From the founding of Jamestown to the time of the
Revolution some 300 silversmiths practiced in the three
cities of Boston, New York, and Philadelphia alone.
Another 200 worked in the smaller centers of New England
and the middle colonies and in such southern places as
Charleston, Annapolis, and Williamsburg. Unfortunately,
if any of these 500 colonial silversmiths left a written
account of his shop practices and methods of work, it has
not been found.
Accordingly, our knowledge of the ways in which colonial
smiths worked is derived from other sources. Most of it
comes from a few technical handbooks and illustrated
encyclopedias published in Europe at about the same time.
Inasmuch as many colonial silversmiths gained their knowledge
of the craft and of its standards of good practice as
apprentices in the old country, it is probable that silversmithing
practices in America were similar.
Not identical, though. The environment of the new
country altered in some manner or to some degree almost
every single attitude, habit, and craft practice. For
example, in eighteenth-century England the silversmith
whose shop was located within the purview of an assay
office could sell the articles he made (with certain exceptions)
only after the pieces had been assayed and stamped
with the appropriate hallmarks, including one denoting the
fineness of the metal. Since the colonies had neither assay
offices nor regulations governing the work of silversmiths,
each smith was responsible for the quality of his own work.
22
Because most re-used plate came originally from England
and because coins were generally minted at or near sterling
fineness (925/1000ths fine, or 92.5% pure silver, the rest
of the alloy being copper), most American silversmiths presumably
turned out work that was not too far from sterling
purity. They could not afford to slip much below that level,
after all, since they competed for favor and sales with the
much esteemed plate imported from England. In many
advertisements in the colonial press, smiths explicitly warranted
their work to be of sterling quality. However, among
the pieces of early American silver that have actually been
assayed in recent years, only a portion have met the test;
quite a number have not.
While American smiths no doubt resented the general
preference of their customers for articles of English manufacture,
they could not overlook the fact that English
fashions in design dominated colonial life. Accordingly,
silver of colonial make imitated the London styles in plate,
being usually some years behind them.
But the American designers were neither unimaginative
nor slavish imitators. Their designs modified the English
originals rather freely—usually in the direction of simplicity
and utility. American silver, dispensing with the heavy
ornamentation for ornament’s sake that often characterized
the work of London silversmiths, tended to be substantial,
serviceable, and vigorous in form, befitting the environment
in which it was to be used.
Acquiring a complete set of Silversmith tools, or at least
a reasonably adequate set, must have been something of a
task in itself. When John Coney, a leading Boston silversmith,
died in 1722 at the age of 67, the inventory of his
goods reflected his many years at the craft. Among the
articles listed were 116 hammers, 127 nests of crucibles, 80
anvils of different shapes and sizes (some called “stakes”
and “teasts”), and unnumbered punches; plus chisels,
swages, stamps, vises, files, and an almost endless variety
of other tools.
23
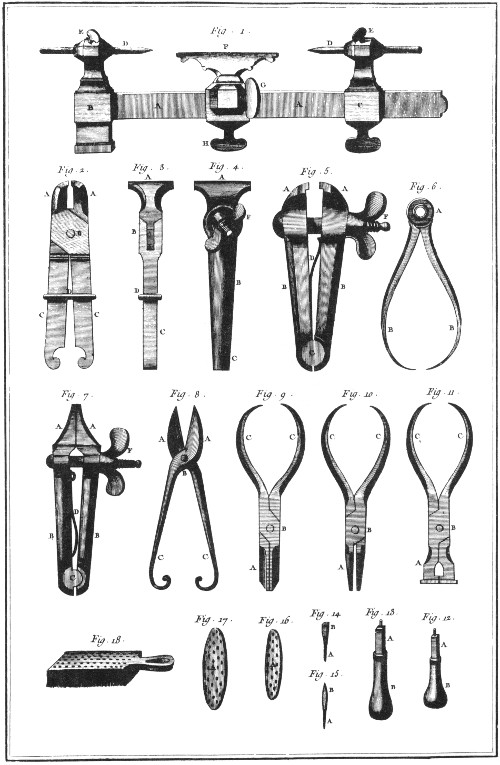
Various hand tools used by the silversmith, including a small lathe, vises, clamps, caliper,
shears, and pliers. DIDEROT.
24
John Burt, another Boston silversmith of the eighteenth
century, got along with only 40 hammers, 15 pairs of tongs
and pliers, 37 “bottom stakes,” 155 punches, and other
tools in like sparsity. A glance at the illustration on pages
27 and 28 from Diderot’s Encyclopedia (published in
France, 1751-1772) indicates the infinite diversity of anvils
that would be needed to produce every possible shape and
size of hollow ware.
Even with all these tools—plus forge, ingot molds, drawing
bench, binding wire, and many other essentials of the
craft—the silversmith was limited to six basic methods of
working silver. These were casting, forging, raising, hollowing,
seaming, and creasing—the principal methods still
employed by hand craftsmen today.
But forging, raising, hollowing, and creasing are all hammering
processes, though they differ significantly in the
manipulation of the metal under the hammer. In essence,
thus, there are only three techniques of forming silver into
an article of desired shape: casting the molten metal in a
properly shaped mold; hammering an ingot into the shape
desired; and building the desired shape from smaller pieces
soldered together. Wire produced on the drawing bench
might be one of these smaller elements. Filing is considered
to be a finishing rather than a forming process.
These forming and working processes, as they would have
been used by an eighteenth-century silversmith, will be
described in more detail in a moment. But the smith,
before he could do any work, had to acquire a supply of
refined metal, probably from his customers. He then
charged them only for his services in fashioning the new
pieces, either a set amount for the type and size of article
or a fixed fee per ounce of silver in the finished article.
Early in the Revolution, for example, General George
Washington ordered a set of 12 silver “camp cups”
from the Philadelphia Silversmith Edmond Milne. He
supplied Milne with “16 silvr Dolls” to make the cups out
of. Possibly these were Portuguese or Brazilian crusadoes
25
or “cross dollars.” As it turned out, there were 1¾ ounces
more silver in the 16 dollars than Milne needed for the 12
cups. He retained the excess for his own use and credited
its value against his charge for workmanship.
Coins went directly into the smith’s “black lead” or
graphite crucible. Old plate had to be broken up first
into pieces of suitable size. Then the crucible was set
down into—not on—the charcoal fire in the forge. Charcoal
on top of the melting silver kept it from absorbing
too much oxygen.
Pure silver is a highly ductile and malleable metal with
the relatively low melting point of 1761 degrees Fahrenheit.
Sterling silver melts at an even lower temperature, so only
15 or 20 minutes in the forge, with constant use of the
bellows, would be enough to melt the crucible’s charge.
Most impurities in the metal would be sopped up by the
porous graphite of the crucible itself. The molten metal
was then poured out into a two-piece cast iron ingot mold
or into an open mold called a “skillet.” In either case,
the cooling metal released any oxygen it might have absorbed
in the form of spitting bubbles that left the surface
of the ingot pitted with tiny holes.
If the piece of work to be made was a small ornament, it
would be cast directly in a sand mold formed by the smith
around a pattern of his own making. The acorn-like finials
atop teapots or on the covers of tankards were normally
made by casting, often a dozen at a time.
Perhaps, however, some customer ordered a simple,
straight-sided silver cup, too large to be cast. Our smith
could have made it by any one of three methods and the
result would be the same in size, shape, weight, and appearance.
Generally only another silversmith could hope to tell
which was made by which process: forging, raising, or
seaming.
To forge such a cup the silversmith would have taken a
billet of silver perhaps 3/16 inches thick and from it cut a
disk of the same diameter as the lip of the finished cup.
26
Then by careful and repeated hammer blows, using shaped
anvils of the proper size and curvature, he would pound the
metal into the form he required.
To raise a cup, the smith would start with silver in the
form of a flat sheet as thick (or thin) as he wanted the cup
to be. He would have made the sheet himself, of course, by
beating an ingot to the required thinness. From the sheet
he would cut a disk whose diameter equalled the average
diameter plus the average height of the finished cup. By
carefully hammering the silver just beyond the edge of the
anvil, he would force the metal around the outer part of the
disk to rise and “shrink” until the cup was shaped.
To make a seamed cup the smith would again use thin
sheet, cutting from it a small round piece for the bottom of
the cup and a slightly curved oblong piece to form its side.
He would roll the latter into a somewhat cone-shaped
cylinder and solder together the edges. Then he would
solder the small disk into the lower end of the cylinder so
that the cup was formed. This was by far the quickest and
easiest method of making hollow ware. The silversmith’s
solder is itself composed predominantly of silver.
Whatever method the smith used to form the cup, he
would finish it by a process known as planishing. In this
procedure the small irregularities in the surface of the piece
are carefully hammered smooth by repeated, deft blows
of a flat, polished hammer. The face of the planishing
anvil is likewise polished to mirror-like smoothness. After
planishing would come the filing off of burrs in crevices of
the design, and then an all-over polishing with pumice,
tripoli, and rouge. At this point the piece would have
been ready for surface ornamentation—by engraving, chasing,
or repoussé.
Engraving means the cutting of a design into the surface
of the work; some metal is removed in the process. Chasing
is the impression of a design on the surface by the use of
appropriately shaped punches. Repoussé consists of raising
a design, somewhat like bas relief, by hammering from the
back or inside of the work. In the second and third techniques
the metal is displaced but not removed.
27
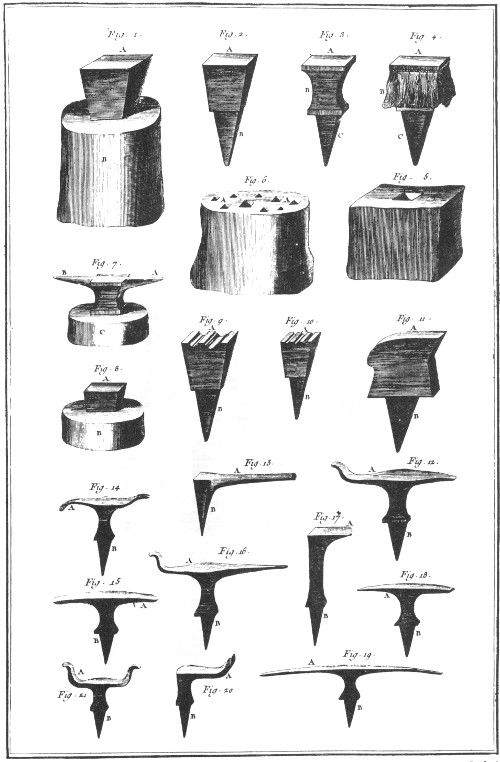
Shown here are a few of the larger anvils and stakes on which the silversmiths shaped their
silver into the finished articles. Since the silversmith had no tool the exact shape of the
articles he made, he had to employ many different shaped tools in the process of manufacture.
DIDEROT.
28
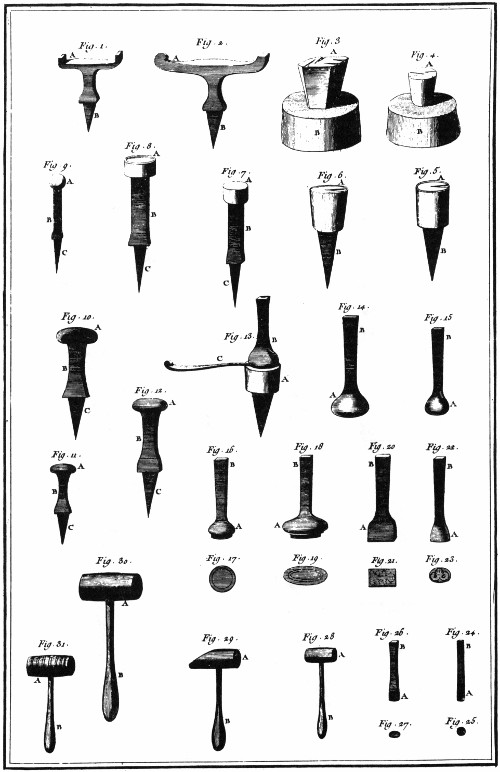
The silversmith often used small anvils, stakes, and dies. Figure 13, for instance, is a spoon
mold used to make the final shape of the spoon. Figures 16, 18, 20, and 22 are button punches
used to impress a design on smaller pieces. DIDEROT.
29
Stamping was normally used only in the forming of such
small articles as the bowls of teaspoons. In this procedure a
piece of silver was forged to the desired thickness and outline,
and placed between a hollowed-out lower die and a
rounded upper one. When the smith forced the two dies
together by a blow of his heaviest hammer, the bowl of the
spoon was formed. By filing, planishing, and polishing—and
possibly some engraving—the one-piece spoon was
quickly finished.
A soup ladle, having a much larger and deeper bowl,
would have been formed by the raising process, with the
handle made as a separate piece and soldered to the bowl.
In fact, only the simplest articles and the smallest ones
could be formed by one process alone. The accomplished
colonial silversmith had to be able not only to refine and
assay his own silver, but to work it up in any combination
of techniques that the design made most appropriate.
As an example, the body and spout of a teapot might each
have been formed by the seaming process, the base by
forging, the top by raising, the finial by casting, and parts
of the hinges by drawing. Then all the parts would have
been soldered together and the piece planished, polished,
and finished off with engraved, chased, or repoussé decoration—or
a combination of these. Finally, the smith would
have attached a wooden handle, which he might have obtained
from a cabinetmaker—or made himself.
Among the silversmith’s final procedures would have
been the stamping of his mark, his initials, or his name on
the piece. This practice of identifying the maker of an
article of gold or silver ware is of long standing, though
perhaps not so ancient as the custom by which a painter or
sculptor signs his work.
Since the year 1300 the Worshipful Company of Goldsmiths
of the City of London has been charged by the
British government with assaying gold and silver wares
30
and coins, and certifying that the metals are of required
fineness. Throughout most of this long period the hallmarking
of English silver articles has retained a basic continuity
of tradition. Disregarding certain modifications and
accretions (some noted in the caption above), every piece
of sterling silver made in England since 1544 has borne
four marks stamped on the back, bottom, or side.
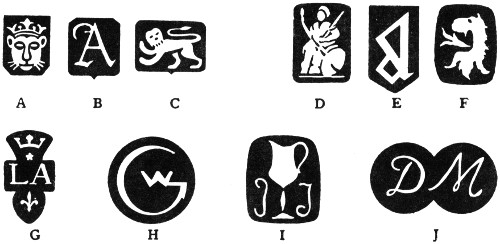
The hallmarks in the first line above and the maker’s marks in the second line
illustrate the variety of markings used on English silver. The leopard’s head
crowned (A) became the mark of the City of London; B and E are date letters; C
is the lion passant denoting silver of sterling fineness. During the Britannia standard
period (1697-1719), the lion’s head erased (F) replaced the leopard’s head crowned,
Britannia (D), still optional, replaced the lion passant on London silver, and the
standard of fineness was raised from 92.50% to 95.83%. Also, the law required the
maker to use the first two letters of his last name, for example (G), the mark of
Paul de Lamerie. It was the custom before and after this period for silversmiths to
use initials. The marks of George Wickes, John Tuite, and Dorothy Mills are
shown (H, I, and J) and examples of their work are in Colonial Williamsburg’s
collection of English and American silver. Some of George Wickes’s tools may be
among those currently used at the Golden Ball and the Geddy Shop.
One is the true hallmark, the symbol of the guildhall
where it was assayed. That of the guild of London goldsmiths
is the head of a leopard and has been in use for the
nearly seven centuries since 1300. Assay offices established
later in a few other cities use other symbols.
Another is the maker’s mark, which has been required
since 1363. This mark is now always the maker’s initials,
but once was more often his trade symbol.
In 1478 a system was adopted of dating each piece assayed
by stamping it with one letter of the alphabet. For this
31
purpose a twenty-letter alphabet is used, the design of the
letter or of the surrounding panel being changed every
twenty years.
Finally, the mark of English sterling standard fineness—a
lion passant—has been used (with one twenty-three-year
interruption) since 1544 to certify that the metal is 92.5 per
cent pure silver. English silver rarely bears the word
“sterling,” which is commonly found on modern American
silver and on that made in some other countries for sale to
Americans. Hallmarking of British goldware is somewhat
different.
Colonial American silversmiths did not adopt the elaborate
marking tradition of the Old World. In the English
colonies no legal requirements existed for marking of any
kind, the guild system was not transplanted, and until 1814
there was not even an assay office. So colonial smiths put
only their own mark on their work. At first this was composed
of the maker’s initials only, but later became more
often his surname, with or without initial. Some smiths also
used a symbol—John Coney the figure of a rabbit, for example—but
this was comparatively rare. Of the Williamsburg
silversmiths we have positive or presumed maker’s
marks of only two—James Geddy and Alexander Kerr.