Up to the end of the eighteenth century the manufacture of
chocolate was carried on entirely by hand, a method at once laborious
and inefficient. The workman used to kneel down on the ground, and
crush the beans in iron mortars. It was not until 1732105 that Buisson
introduced the use of a bench and so rendered that inconvenient and
unwholesome practice unnecessary. Even to-day, the Chinese cooks
on the Philippine islands carry their chocolate “Factory” about with
them, in which the trestle is essential. It further comprises a small
marble mortar and warmed pestle, and by means of these utensils and
implements the hulled beans are pounded, and the triturated mass so
obtained spread out. It is then flavoured with sugar and spices. With
that exception, hand labour in the chocolate manufacture has since
the year 1778 been entirely displaced by machinery, when Doret
exhibited the first specimen before the medical faculty of Paris.
According to Belfort de la Roque,106 a Genoese named Bozelly had
already constructed a mill by means of which he was able to prepare
from six to seven hundred pounds of chocolate daily, comparing
favourably with the thirty pound output yielded by hand labour.
Pelletier107, in 1819, describes a machine for the mechanical preparation
of chocolate of his own construction, capable of doing the work of
seven men. The machines used in the chocolate manufacture have
since that time been repeatedly improved and re-constructed, although
always with this one end in view, namely to obtain a fine even cacao
mass, and afterwards mix it as thoroughly as possible with the other
ingredients employed.
The first machines of the modern type were constructed by the
Parisian mechanic George Hermann (1801-1883) in the year 1830, to
which inventor we are indebted for the principle of fine grinding with
varying velocities, on which manufacture of chocolate is based
to-day. There is at the present time a rather large circle of manufacturers
engaged in the putting together of special machines for the
preparation of cacao and cacao products, chocolate apart.
Whether chocolate manufacture be carried out on a large or
small scale, it always involves the subjecting of the cacao bean to
a regularly succeeding series of operations, before the resulting
product known as “Chocolate” (in the strict commercial sense of
the term) can be obtained.
The respective operations succeed each other as follows:
I. Preparation of the Beans.
1. Storing, cleansing and sorting of raw beans.
2. Roasting the cleansed beans.
3. Crushing, shelling and cleansing the roasted bean
(removing the radicles etc.)
4. Mixing different kinds of beans.
II. Production of the Cacao Mass.
5. Grinding the beans till they yield a homogenous paste on
heating.
6. Mixture of the liquefied cacao mass with sugar, spices, etc.
7. Trituration by rollers.
III. Preparation of the resulting Chocolate.
8. Extraction of air, division and moulding.
9. Cooling.
10. Packing and storing.
This represents the general course of manufacture, which we
will now proceed to describe in more detail, following the headings
given above.
1. Storing, cleansing and sorting.
Right up to the moment when they are to be used in the
manufacture, the raw cacao beans must be kept as originally packed,
and stored in an airy sun-lit room; although if they have accumulated
moisture during transport or sustained any manner of damage in
harvesting, they should then be emptied out of the sacks, spread out
over the floor of such a room as above described, and dried as
effectively as possible. It has also been recommended that such beans
be washed with a dilute solution of caustic potash (1 in 5000), and
afterwards dried rapidly.
Unfermented beans, those damaged in the harvest, and those
which have received no proper fermentation, develop a greyish
white colour with occasional tints of violet and an unpleasant, bitter
herbal flavour, properties which unfortunately penetrate to the resulting
cacao products. Attempts have been made to meet this evil
with a so-called “Secondary Fermenting Gordian108 proposes in
this connection that the beans be filled in water-butts, and steeped in
warm water for at least 48 hours (so that obviously the butts must
be kept in a warm room), at the expiration of which time it can be
poured off, and the beans dried in a chamber heated to a temperature
of between forty and fifty degrees centigrade. There is said to
ensue an appreciable improvement as to flavour and colour, when
this process is carried out.
The magazines in which cacao beans are stored have sometimes
an unwelcome visitor, to wit, a grub which according to W.
Hauswaldt109 happens to attack just the best kinds of Caracas and
Trinidad. As eggs of the grub have on several occasions been
found on the interior of the still unshelled bean, we may assume
that they were deposited by a butterfly (species unknown, but
possibly Ephestia cahiriteller, cf. von Faber loc. cit. page 335) either
before or immediately after fermentation, and no later. Sometimes
these grubs appear on the surface of the sacks, which they
overspread in a few days. Removal of the infected packages, opening
the sacks, and exposure to the sun, as well as a thorough cleansing
of the storehouses, is attended with a qualified amount of success.
The best plan is to destroy the moths during their period of activity
in the summer months June, July, and August.
According to Hauswaldt, Stollwerck110 and G. Reinhardt111, this
can be effected by placing in the store rooms large, shallow basins
of water, near which burning petroleum lamps are introduced on the
approach of dusk, favourably placed on a pile of bricks and stone,
so that they clearly illuminate the reflecting water. The moths
assemble round the light en masse and either perish in the water or
flame, a fate which sometimes overtakes even the larvae, for they
display the same fatal attraction for any light, real or apparent. The
water must be changed every day, as otherwise the wing-dust
collecting on its surface affords a means of escape to the insects
coming later. As the weather becomes cooler, the doors and windows
of the store-rooms should be left open, so that when frost sets in,
the rest of the maggots may be destroyed.
The cleansing and sorting of the raw cacao bean is the most
important factor in the manufacture of chocolate, and yield a
manifold return, for inferior and cheaper kinds of bean which have
passed through these processes can be advantageously mixed with
finer varieties. The chief object of cleansing and sorting is the
removal of foreign bodies and such chance admixtures as sand,
pebbles, and fragments of sacking, which are liable to damage the
stones used in grinding at a later stage of the preparation, or communicate
an unnatural and disagreeable smell to the subsequent
roast products. These admixtures are so multiform and various that
they cannot be removed solely by the aid of machinery, but must
be finally picked out by hand. Mechanical appliances are limited to
the removal of pebbles, dust, and possible fragments of iron, after
which preliminary cleaning the beans are thrown on straps, where
they can be picked by hand. The collector of these foreign bodies
would find himself with a rather interesting stock at the end of a few
years, as Wilhelm Schütte-Felsche points out.
The cleansing of the raw beans was formerly carried out in so-called
roller casks, placed horizontally, and revolving round an axle
fitted in the floor, whence it passed upward, cutting them slantwise.
In this apparatus the beans were rolled and vigorously rubbed
together, and afterwards the hand-picking succeeded. More recently,
the roller casks have been displaced by rotary cylindrical sieves,
driven by motor power.
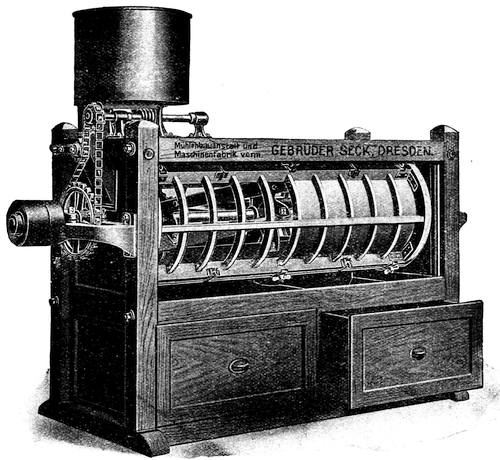
Such a machine is illustrated in fig. 12. The beans are lifted
to a rotatory cylindrical sieve by means of an elevator, where they
are freed from dust and dirt; in other sections of the sieve fragments
of blossom, sacking, or cloth are isolated, whilst occasional splinters
of iron are removed by a large magnet. So prepared, the beans are
cast on running belts, and here the hand-picking above-mentioned is
carried out.
Fig. 13 shows a cleansing machine for the same purpose, which
has recently become rather popular. Here the dust passing from the
sieve is sucked up into a dust chamber, by means of an exhauster,
whilst pebbles, blossom fragments, and small beans are separately
isolated. The cleansed beans pass likewise under magnetic influence,
which removes traces of iron, and finally succeed to the running
belting.
Often the beans are introduced into an extensive brushing
machine before roasting, to cleanse them from dirt etc. These are
generally found in such factories as have circular and cylinder
roasters with direct heating apparatus. Fig. 13 a shows such a
brushing machine for cacao beans.
2. Roasting the Beans.
The cleansed and sorted beans are now subjected to a high
temperature, that is to say, they are now roasted. This roasting
answers many purposes;
1. The aroma and flavour of the bean is so developed.
2. The starch granules are gelatinised.
3. The herbal constituents are so transformed that the flavour of the
beans becomes milder; a distinct improvement.
4. In the consequent drying, the shells are rendered brittle, and more
easily removeable.
5. The beans themselves can afterwards be better ground.
The roasting of the cacao bean does not demand so high a
temperature as that of coffee, to effect the above chemical and
physical changes. Experience has shown that the best temperature
lies between 130-140 ° C., though deviations from this standard
have recently become frequent and considerable, according to the
uses for which the cacaos are intended, and roasting has sometimes
taken place at a temperature even as low as 100 ° C.
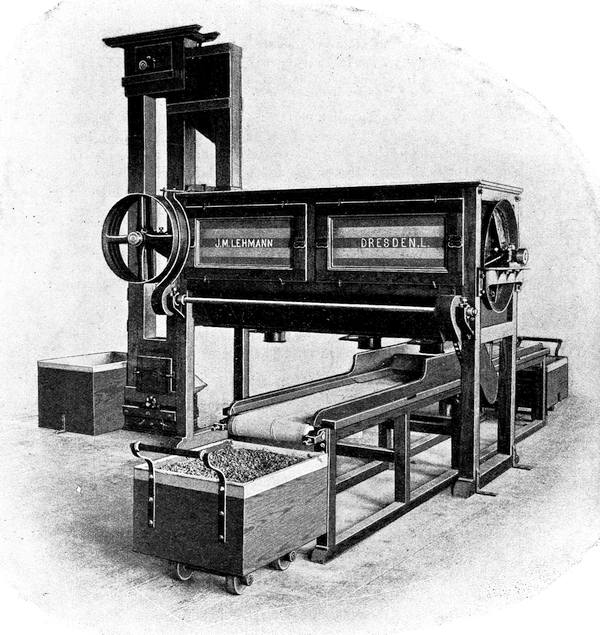
Fig. 12.
The process of roasting can be carried out in the roasting
drum or machine in a variety of ways, as:
1. Direct roasting over a coal fire,
2. Passing of a hot-air stream over the beans,
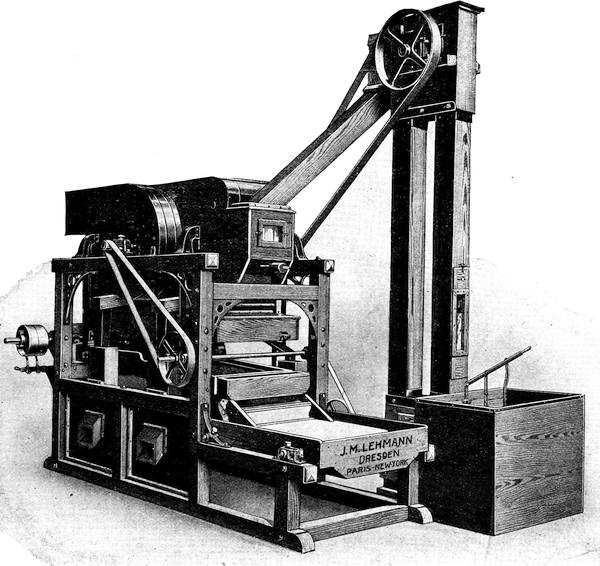
Fig. 13.
3. Roasting by means of gas, with compressed air, as far as
sources of heat are concerned; and as regards shape of
the drum, it is to be noted that the cylindrical are most in use.
The separation of the shells from the kernel was still effected at the
beginning of the present century by stirring the beans in water and
so detaching the inner coating of the seeds, the method adopted by
Weisched (Mitscherlich page 112). Not till this stage had been
reached were they subjected to a strong heat, causing the shells to
spring off.
This method has at the present time only historical interest,
for the so-called roasting drums, as used in the preparation of coffee,
are now universal.
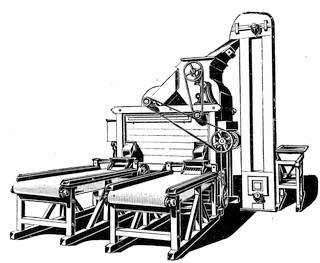
Fig. 13a.
Roasting must be attended with the greatest care, in order
that it may neither be too thorough nor insufficient. It is a great
mistake to think that the roasting machine can be handed over to the
care of any apprentice. That nicety of roasting which corresponds
to the variety and its subsequent utilisation constitutes the qualitative
basis of the chocolate manufactured later. It is impossible for
even the best chocolate maker to retrieve what has been spoilt
in this important preliminary operation, wherefore a skilled workman,
endowed with a keen sense of taste and smell, is always to be seen
at the roasting machine.
It has already been attempted to provide a means of security
against over-burning by the construction of the so-called safety-roaster,
about which will be spoken later.
Overroasting is immediately indicated by a disagreeable empyreumatic
odour (resembling that of roasted coffee); the husks
char and the kernels crumble, also betraying a charring on the
outside. There is a correspondingly increasing keenness of flavour,
and a transference of theobromine from the kernel to the husks
(cf. page 65). From the destructive distillation of the cacao fat arises
that volatile and pungent acroleine which is the principal cause of
the empyreuma of the over-roasted bean.
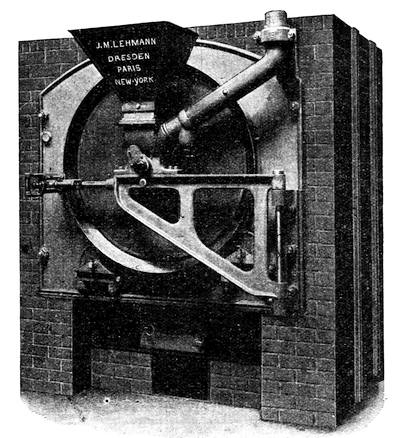
Fig. 14.
The following general precautions in roasting cacao are worthy
of note; 1. the beans should not remain too long in the roasting drum;
2. they should be kept on the stir, for which reason the apparatus
is made revolvable on its axles; 3. the heat applied should be carefully
regulated; and 4. to guard against a loss of aroma, the roasted beans
should be cooled as rapidly as possible.
As the cacao must be more or less roasted according to its
quality and ultimate destination, which entails the acquisition of considerable
empirical knowledge on the part of the workman entrusted
with this process, it would be neither advisable nor practicable to
annex definite instructions as to time and temperature requirements.
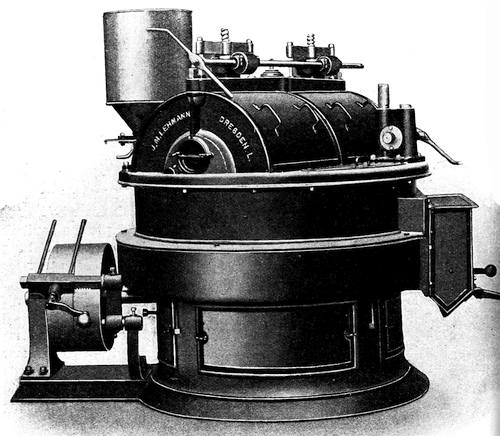
In the following we describe a machine which is to be found
in most factories and which corresponds to all the demands of
technique. From its heating system, it belongs to the class of hot-air
current roasters—direct coal fire assisting—and in shape to the
cylindrical roasters.
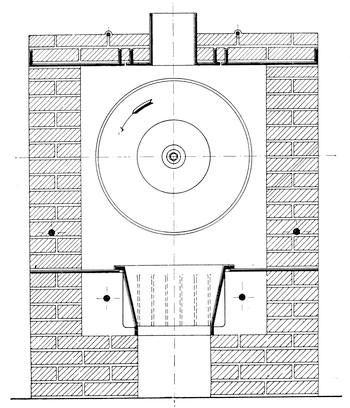
Fig. 14 a.
This machine is illustrated in fig. 14 and shown in section in
figs. 14 a and 14 b. To prevent loss of heat by radiation, to save fuel,
and preclude possibilities of danger from fire, the whole installation
is walled in. Driving shafts occur at the back of the machine, and the
charging apparatus is introduced in front. A furnace lies directly
under the drum, whilst on either side are chambers accessible to
currents of fresh air, which are provided with heating tubes and
which admit of a regulation of the air supply. They are shut off
from connection with the gases from the fire, so that only the fresh
air heated here can penetrate to the roasting products in the charged
drum. There are winnowing shovels fitted in this, calculated to keep
the beans in motion and facilitate the access of air. When the hopper
is closed, the gases arising from the roast product can be led off by
an annexed outlet pipe, and thereupon condensed and the resulting
liquid drained off at the foot of the machine. For the attainment of the
proper degree of roasting, as well as for controlling the whole process,
there is a sampler to every machine. The drum is emptied whilst in
motion, its door-like front being turned aside and the roasted beans
transferred by the winnowing shovels before mentioned to trolleys
wheeled underneath.
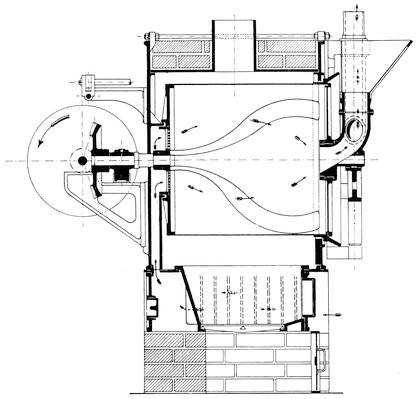
Fig. 14 b.
The loss of heat by radiation is very insignificant, as the
machine is completely walled in. Any kind of fuel may be used.
Since the stoking as well as the removal of soot takes place at the
front, several of these roasters can be set up side by side. It is a
great advantage of this installation, that by removal of the front of the
drum its interior is laid quite open, admitting of a thorough overhauling
which is attended with every disadvantage for the flavour of subsequent
roasting lots.
The machine here described is constructed in varying sizes,
with an outside capacity of four hundred kilograms.
As already mentioned the so-called safety-roaster offers a
certain security against the burning of the beans as the roasting boiler
is lifted out of the fire by means of an automatically working safety
regulator. Figs. 15 a and b show a spherical roaster open and closed.
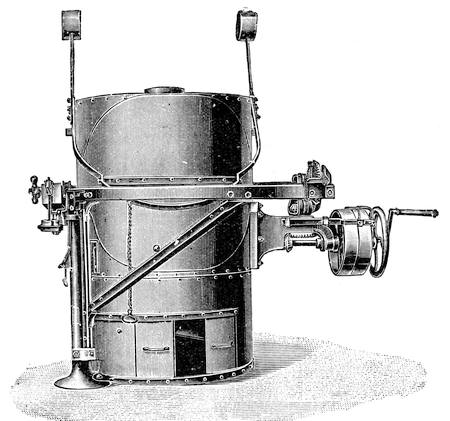
Fig. 15 a.
The principal of construction is founded on the fact that each
roasting is connected with a loss of weight and it is logical that the
same quality of beans always yields the same loss of weight at a
certain degree of roasting. On an average cacao yields a loss of
6-7 %. According to this, the loss of weight which can at first be
empirically ascertained, for example by a new kind of bean, can be
calculated and can be indicated on a regulator, on the principle of the
Roman scale. When the beans have lost the weight in question the
counterpoise of the regulator raises the axle of the roasting sphere by
means of which the working of the whole machine is set in motion.
There is no exception to the rule that only beans of one and
the same kind should be roasted and broken up together, as thickness
or thinness of the shells determines to a large extent the time
required for roasting, and also an even size of bean is necessary to
the smooth operation of the breaking machine. The husks of the
roasted cacao bean are hygroscopic, and consequently the roasted
unshelled beans contain more moisture after having been kept for
a time, than they do in the raw state; but the drier the bean is,
the easier it shells. The cacao is therefore to be worked up as
quickly as possible, or at least kept in well covered metal boxes till
further treatment can be proceeded with.
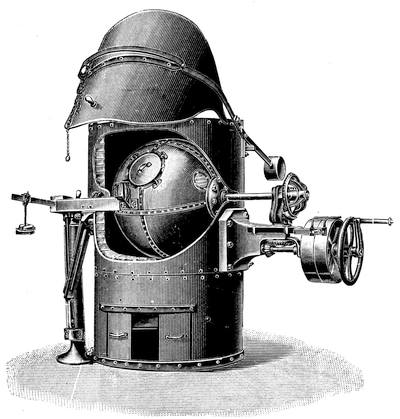
Fig. 15 b.
As sources of heat we find direct and indirect stoking with
house coal and coal gas, and besides these, for the installations of
larger factories Dowson gas is especially suitable, as it does not
involve too high a temperature, and the outlay is not so great as
when coal-gas is used.
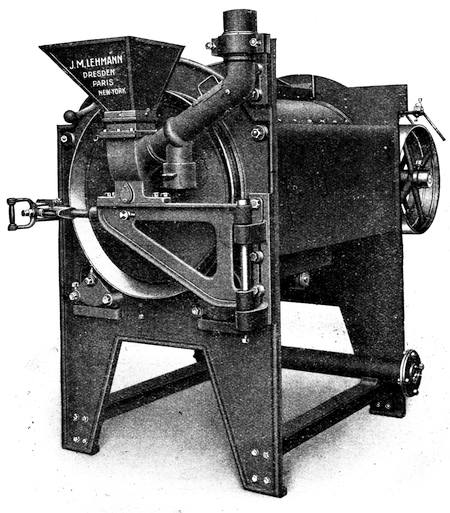
Fig. 16.
The roasting machine in fig. 16 for Dowson or coal gas belongs
to the class of roasters with direct firing. It corresponds to the
one diagrammed in Fig. 15 as regards charging and emptying. Here
also the front wall of the drum can be removed, and the interior
consequently laid completely open. The transmission of gas is
effected at an air pressure of one atmosphere, for the attainment of
which an air pump is fitted up in the vicinity, capable of feeding four
machines at the same time. The drum holds about 150 kilos.
It goes without saying that the regulating of the requisite heat is in
this instance of the utmost ease and nicety. Another preponderating
advantage of this machine as compared with those heated with coke
or ordinary coal is its clean operation and the extraordinary speed
with which it can be both started and stopped. Form 3-4 cbm. of
coal gas are needed for 100 kilos of beans, whilst for Dowson gas,
which has not such a high heating value, much larger quantities are
required, and consequently a stronger framework becomes necessary,
though here no air pumps need be put in operation.
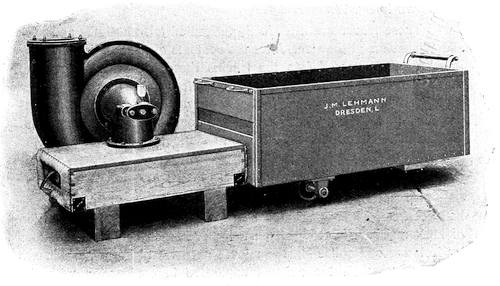
Fig. 17.
Steam roasting apparatus have not proved particularly successful,
as has been evident in all experiments hitherto made with them,
and steam agency does not appear to be suitable for the cacao bean,
it admitting of no thorough and at the same time even roasting.
Yet on the other hand the hot air-current roasters described
enjoy an ever increasing popularity, partly because they are heated
indirectly, and again because they appreciably diminish the time
taken up in the actual process, which in other cases approaches to as
much as thirty or forty minutes, without exposing the beans to the
danger of burning or getting charred.
As just stated, the beans should be passed on to the next
process as speedily as possible, yet on the other hand be completely
cooled off, so as to loosen their shells before they arrive in the
breaking machine. There are also special constructions for this cooling.
If the roasting drums are fitted up directly on the ground, it is effected
by disposing the beans issuing from these machines in wide baskets or
sieves, and letting them cool there before bringing them to the next
process. Should they be situated at a sufficient height, the beans
can be slowly transferred down a shoot connected with the rooms
below, where crushing mills await them, and cooled on the journey
by a play of fresh air currents.
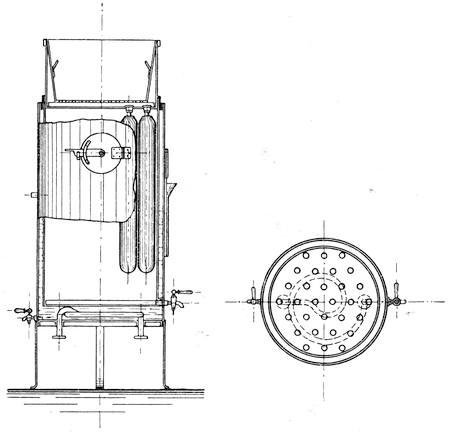
Very much to the purpose and well adapted as regards most
of the requisite conditions, are the cooling trucks with exhaust apparatus
shown in fig. 17.
These trucks are fitted with perforated false bottoms and with
sliding shutters at the side. After the contents of the roasting machine
have been discharged into the trucks, these are wheeled over to
the exhaust apparatus easily recognisable in the diagram, where
the cacao is so far cooled that subsequent “after-roasting” is impossible,
whilst the gases given off are conducted by the ventilator.
This exhaust chamber can be made to work from both sides.
3. Crushing, hulling and cleansing.
Up to ten years ago, the crushing and shelling of cacao beans
had not been so far perfected as to effect the complete separation
of husk and radicle from all particles of kernel, or to prevent loss
by isolating and collecting the minute particles of kernel, which are
drawn up through the exhaust apparatus in conjunction with the
lightest of the cacao shells. Yet the requirements demanded of a
satisfactory machine advanced to such an extent that not only cacao
nibs free from shell were postulated—an end scarcely hard to attain—but
shells free from cacao nibs were made a further essential. A
machine which performs both these objects not only works excellently,
but is also economical. For a solution of this problem the
Association of German Chocolate Manufacturers, which is specially
interested in all that concerns the chocolate industry, offered a prize
years ago; the firm of J. M. Lehmann were the first to construct a
machine answering every call made on it to perfection.
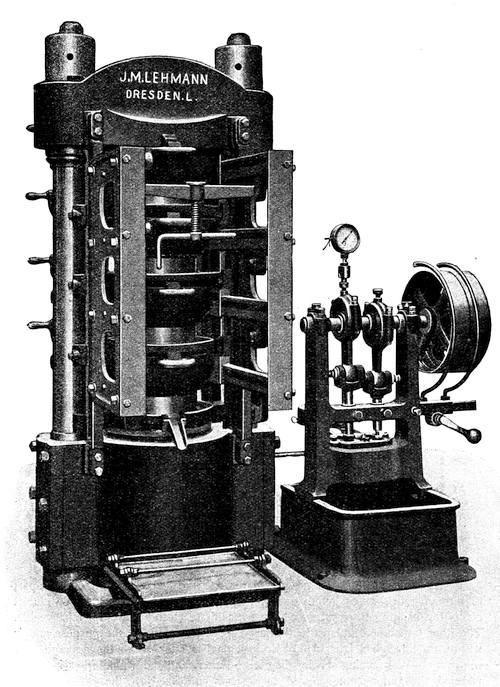
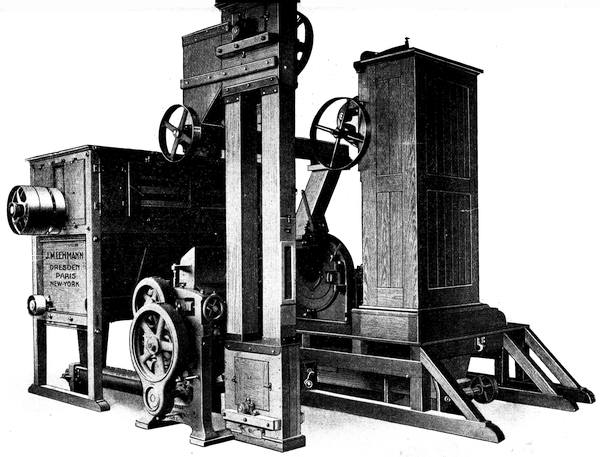
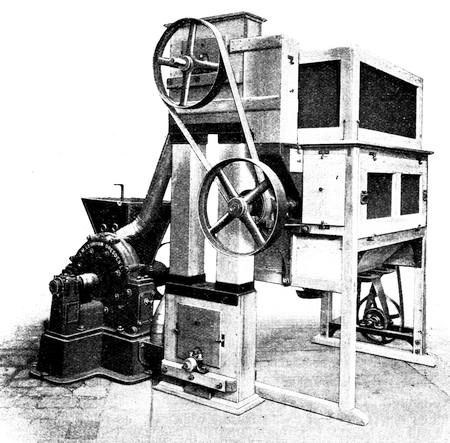
Fig. 18 illustrates a crushing and cleansing machine averaging
an output of 2500-3000 kilos, of the latest and most modern type.
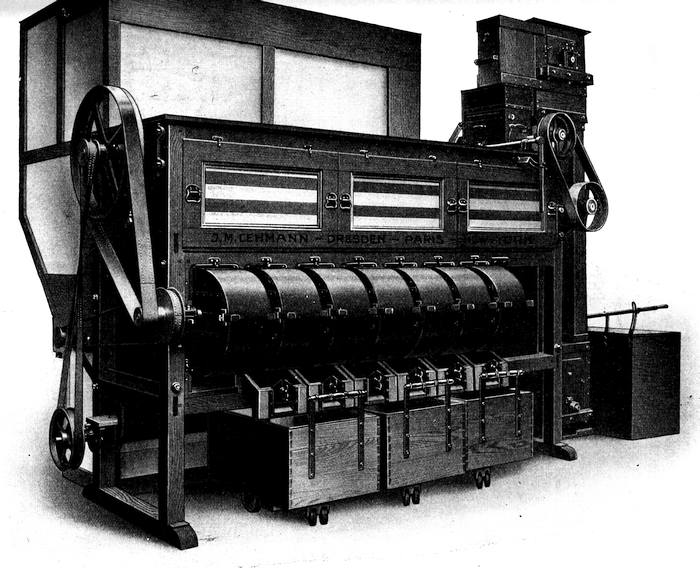
Fig. 18.
The beans are first broken into smaller pieces in all
machines now employed as crushing, shelling or cleansing apparatus,
and the one at present under consideration provides no exception.
An air-current is made to play on these fragments, which finally
isolates and transfers the loosened shells to another part of the
apparatus. The cacao next succeeds to a crusher of regular capacity
lodged in the upper part of the machine, being despatched on an
elevator. The fragments fall into a cylindrical sieve, dust being
detached in the first compartment, whilst the meshes of subsequent
compartments gradually increase in size and sort the products therein
transmitted in corresponding sizes. There is a groove traversed by
air-currents—proceeding from a ventilator—immediately under each
compartment. This current of air can be regulated, i. e. made weaker
for lighter and stronger for heavier fragments, and there is a ventilator
for every compartment to make this regulation of the easiest,
and in this way shells of equal size but specifically lighter than,
the cacao fragments are most efficaciously separated. Contrasting
with the older type of machine, it works almost noiselessly, all
shakings of grooves and sieves being entirely avoided; in addition
to which there is a perfect exclusion of dust, when the shells are
transferred into the dust-removing chamber. A further advantage is
that there is no wearing out of the machine, except as regards the
direct crushing apparatus, which occasionally need renewing.
The dust particles before mentioned, which possibly comprise
as much as one half of the cacao fragments, require a special kind
of working up, on different machines, before the cacao still
contained therein can be obtained. It is a fact obvious and apparent,
that the smaller the fragments of shell mixed with this crushed cacao,
the more difficult will be their separation, a fact of equal importance
to technical and analytical science, and the more scrupulously this
process is to be carried out, the greater the lavishment on sieves
and ventilating compartments entailed.
To effect this operation on the breaking machine is seriously
to overtask the latter, and defeats its own end, as experiments carried
out in the Chocolate factory of Schütte-Felsche have proved,
inasmuch as it leads very easily to mixing of the products which are
to be kept separate.
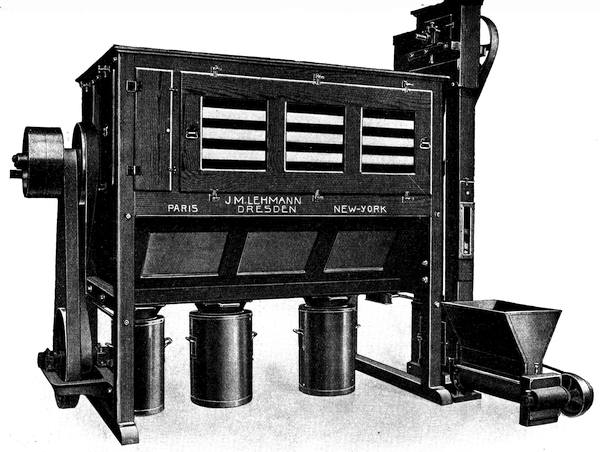
Fig. 19 shows such a machine for the cleansing of this so-called
cacao “dust
The particles are raised to a large flat sieve by means of
an elevator, again sorted in different sizes, and submitted to air
currents of corresponding strength. The quantity obtained varies
according to the variety of cacao, though in some cases it may
amount to 50 or 54 percent. What remains after this process is absolutely
worthless and can only be considered as refuse, at least as
far as the chocolate manufacturer is concerned.
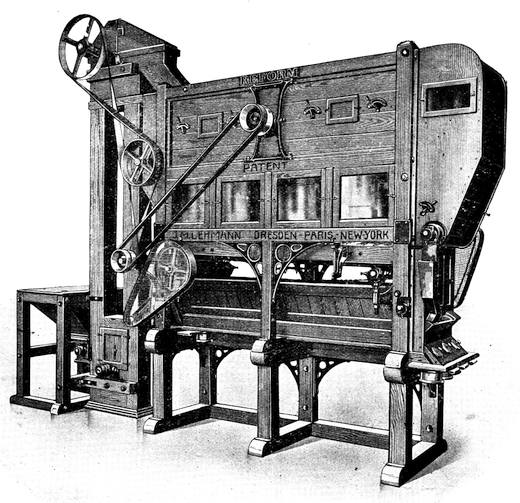
Fig. 19.
It has become necessary in modern manufacture that iron
fragments occurring in the machine not only be separated by
distinct magnetic fields in the respective machines, but that this also
be effected in a machine specially constructed for the purpose.
Fig. 20 illustrates such an electromagnetic apparatus. The advantages
of this system are that it avoids magnets limited in strength,
and by the functioning of strong electro-magnets perfect cleansing
even in the case of the largest output, as well as machines of
the most simple construction, can be guaranteed.
We submit the following description of the machine and its
method of working.
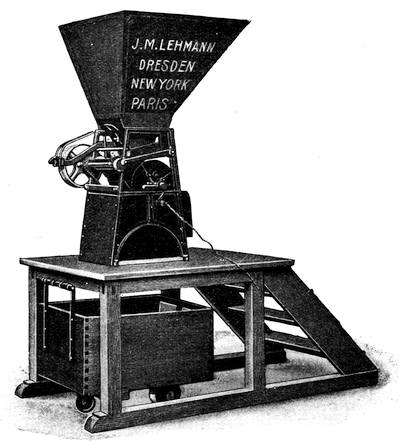
Fig. 20.
The machine contains a hopper with sloping groove to obtain
an even introduction of the beans to be cleansed. At the end of this
there is an electro-magnet roller, consisting of a non-magnetised
mantle and a magnetic compartment round which it turns.
After traversing the sloping groove, the beans succeed to
the roller, meeting it at a tangent. As soon as they reach the field
of magnetism, all iron fragments are appropriated by the revolving
mantle, whilst the beans themselves do not come into contact with
this, but pass directly underneath. The iron fragments are disposed
of separately, and outside the magnetising area.
It is of prime importance in the preparation of chocolate and
more particularly of cocoa powder (easily soluble cacao), that the
crushed material proceeding from the crushing machine should
undergo a further purification, with a view to separating, and removing
the hard radicles. These constitute the gritty sediment of
insufficiently prepared cacao powder, when dissolved. J. M. Lehmann
effects the complete removal of the radicle by means of his machine
D. R. G. M. No. 24,989 (Fig. 21).
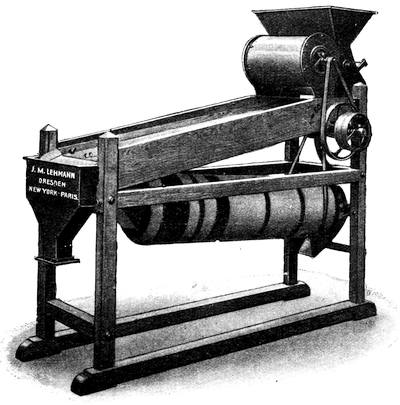
Fig. 21.
Here the finer siftings from the crusher are transferred to the
controlling feeder, under which a small ventilator occurs, which
provides for the removal of any still remaining portions of husk.
Cacao and radicle descend to a shaking sieve, the finer particles
passing through its meshes, whilst the larger grains fall into a pocket
attached to the end, as cleansed product. The former fragments
now succeed to a cylinder, having its inner surface punched with
small cavities (fig. 22) and while the cacao particles remain in those
cavities during the rotation of the cylinder, the radicles of more
elongated form are caught up by a special separator (1) and so prevented
from being carried round with the rest. The cacao particles
are then made to fall into a trough (3) by a brush (2) working
against the cylinder, and subsequently urged forward by a conveyor
(4). That process is enacted all along the cylinder, so that finally
cacao and radicle issue from the machine completely separated.
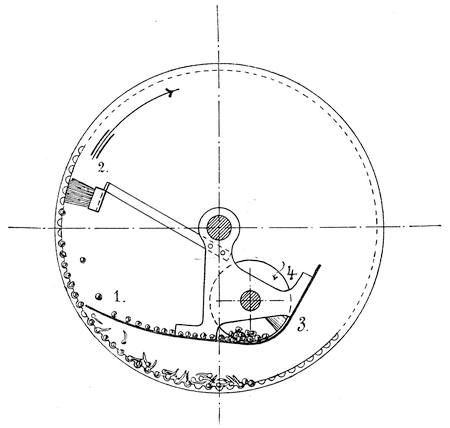
Fig. 22.
The advantages, economical and otherwise, attending the use of
the above breaking and cleansing machines become apparent when
the following figures, registering results obtained in several experiments,
are considered. Formerly the loss experienced in sorting,
roasting, crushing and hulling averaged about 30 % of the total beans,
but now the employment of the above machines shows the following
satisfactory improvements.
The loss of 823 kg Machala beans, unroasted, amounted to
a total:
| a) in picking |
3·6 |
kg |
| b) " roasting |
63·5 |
" |
| c) " shelling |
61 |
" |
| d) " dust |
34 |
" |
|
162·1 kg or 20%, |
without taking into account the application of the waste; 2267 kg
of St. Thomé raw cacao lost:
| a) in picking |
5 |
kg |
| b) " roasting |
170 |
" |
| c) " shelling |
152 |
" |
| d) " dust |
79 |
" |
|
406 kg or 20%. |
According to these data the use of these machines admits of
a saving of about 10 percent more material than in former work.
In connection with these particulars it is also of interest to
consider the qualitative and quantitative composition of the various
waste products of the manufacture. Filsinger112 has at the instance of
the Association of German Chocolate manufacturers, examined a
mixture of 50 pounds of large Machala beans with an equal quantity
of small beans, after passing it through a shelling machine of the most
modern construction, and he thus obtained:
| 70 |
pounds |
of |
large kernels, |
| 9·2 |
" |
" |
medium kernels, |
| 0·8 |
" |
" |
radicles, |
| 10 |
" |
" |
husk (outer woody shell), |
| 4 |
" |
" |
cacao waste, |
| 6 |
" |
" |
other loss, |
The 4 pounds of cacao waste yielded by further sifting:
| a) kernel |
I. |
sort |
250 |
grammes, |
|
II. |
" |
50 |
" |
|
III. |
" |
220 |
" |
|
IV. |
" |
25 |
" |
| b) husk |
I. |
" |
185 |
" |
|
II. |
" |
55 |
" |
|
III. |
" |
370 |
" |
|
IV. |
" |
80 |
" |
| c) cacao dust |
725 |
" |
| d) waste |
30 |
" |
| e) loss |
10 |
" |
|
2000 grammes. |
Chemical analysis of these portions gave the following results:
|
Percentages |
| Ash |
Sand |
Fat |
Fibre113 |
| 1. Husk 10% of the raw cacao |
11·15 |
1·90 |
4·50 |
21·36 |
| 2. Cacao waste 4% of the raw cacao |
4·80 |
0·35 |
15·40 |
16·31 |
| 3. Seed shells I. sort ;0·37% of the raw cacao |
6·70 |
— |
21·64 |
10·29 |
| 4. Seed shells II. sort 0·11% of the raw cacao |
7·10 |
— |
18·39 |
8·75 |
| 5. Seed shells III. sort 0·74% of the raw cacao |
7·20 |
— |
15·76 |
12·16 |
| 6. Seed shells IV. sort 0·16% of the raw cacao |
7·80 |
— |
16·40 |
12·74 |
| 7. Cacao dust 1·45% of the raw cacao |
11·75 |
— |
22·06 |
8·40 |
| 8. Waste 0·06% of the raw cacao |
7·05 |
— |
20·44 |
9·81 |
From these data it is evident that there is a great difference
between the chemical composition of the so called cacao waste
and that of the exterior ligneous shells. From the large amount of
fat present in the former material it might be regarded, in the full
sense of the term, as a cacao constituent and, for that reason, its
presence in cacao preparations should not be objected to, while the
husk containing as much as 20 percent of woody fibre cannot be
considered a cacao constituent in the same sense.
4. Mixing different kinds.
Stress has already been laid on the variations in taste incidental
to different species of bean. It has further to be noted that they
develop a milder and more aromatic flavour according as they have
been more properly fermented, and in contrary instances possess an
astringent and even acid taste. It therefore becomes an aim of the
manufacturer so to improve the flavour of inferior varieties by
mixing with the finer as to produce a resultant cacao giving perfect
satisfaction to every taste. Nevertheless the general rule still holds
good that for the preparation of the finest qualities of chocolate only
the better sorts of bean (as Caracas, Ariba, Puerto Cabello etc.) should
be employed. For inferior and less expensive ware other varieties
of bean suffice, the mixture being obviously regulated by the prevailing
market prices.
In many instances the proportions of such mixtures are kept
secret by the manufacturer as matters of importance, and every
individual manufacturer has his own method and specialities as
regards such blends.
We compare here a few verified blends:
| 1. |
2. |
| Caracas |
}of each 1 part |
Caracas |
= 1 part |
| Guayaquil |
Bahia |
= 5 parts |
| 3. |
4. |
| Maracaibo |
}each 1 part |
Trinidad |
}equal parts |
| Maragnon |
Maragnon |
| 5. |
6. |
| Caracas |
= 1 part |
1 part Ariba |
| Maragnon |
= 2 parts |
1 part Surinam |
|
1 part Trinidad |
| 7. |
8. |
| 1 part Ariba |
3 parts Ariba |
| 1 part Trinidad |
1 part Trinidad |
| 1 part Surinam |
1 part Surinam |
| 1 part Caracas |
1 part Caracas |
| 9. |
| 1 part Machala |
| 1 part St. Thomas |
Ceylon cacaos are not used so much as mixing varieties, but
almost exclusively as covering agents, to make other cacaos lighter
coloured (sometimes almost approaching yellow).
The beans are weighed off in these proportions on a sensitive
scale, and then passed on to be ground and triturated into cacao
paste.
5. Fine grinding and trituration.
Formerly the roasted, crushed, and decorticated beans were
frequently ground before being transferred to the “Melangeur”,—a
machine that will be described later—, in which they were then
reduced to a finer state of sub-division and lastly mixed with sugar.
For this grinding, mills of various construction were employed (as
Weldon, Pintus etc.). But as time rolled on the Melangeur took the
place of these preliminary grinding mills, and in this it was
endeavoured to effect that fine division of the cacao mass which is
essential to the production of a homogeneous cacao and sugar intermixture,
but without complete success. Cylinder rolling machines
(French method) were the first to attain this result.
At the present time, the roasted and cleansed kernels are
ground so fine as to become a semi-liquid when subjected to heat, and
that is done whatever the ultimate destiny of the cacao, whether it
be intended for chocolate or cocoa powder. This object is obtained
by means of special mills, constructed with “Over-runners
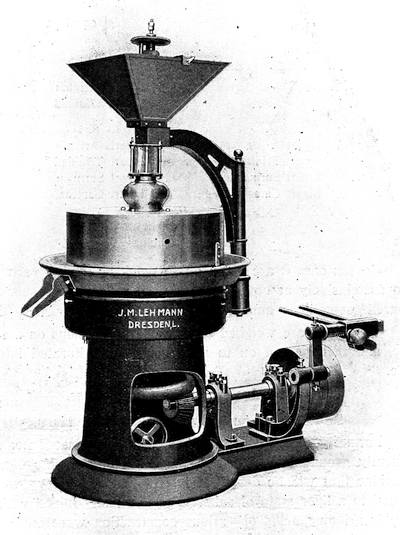
Fig. 23.
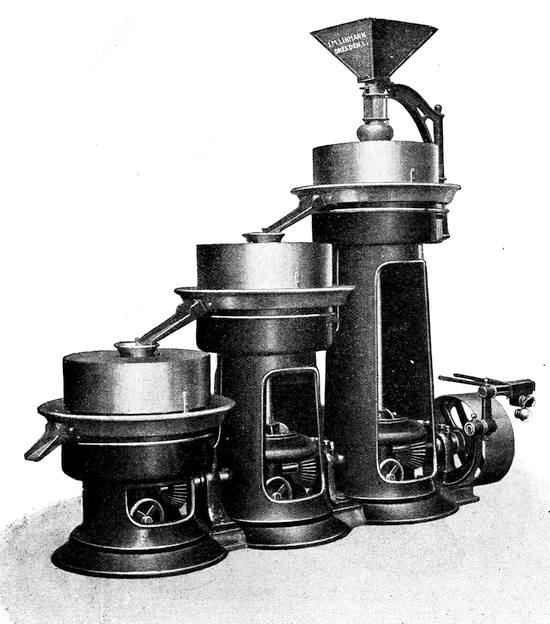
Fig. 24 a.
These cacao mills, which were formerly but seldom met with in
chocolate factories, have now become indispensable necessaries, since
they have the advantage:
1. of rendering the cacao mass in this semi-glucose form more
easily miscible with sugar, a factor of the highest importance for the
commoner and cheaper qualities of chocolate;
2. of grinding the cacao as fine as possible in one operation
and the simplest manner.
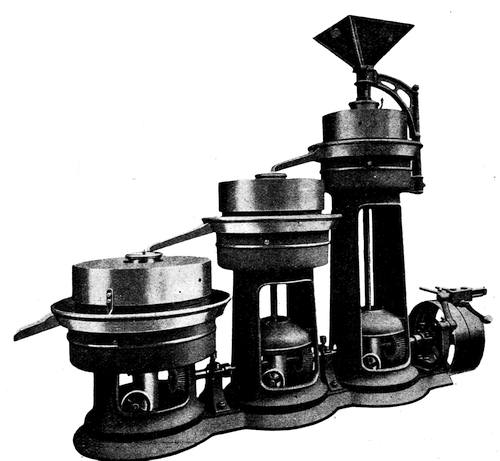
Fig. 24 b.
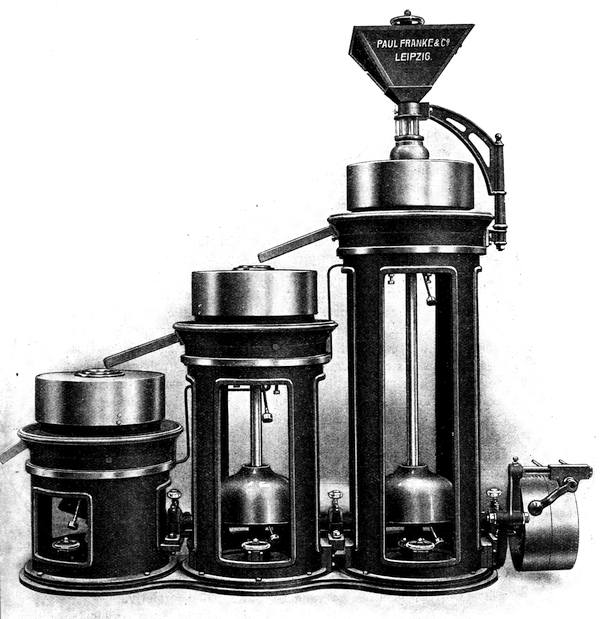
Fig. 24 b.
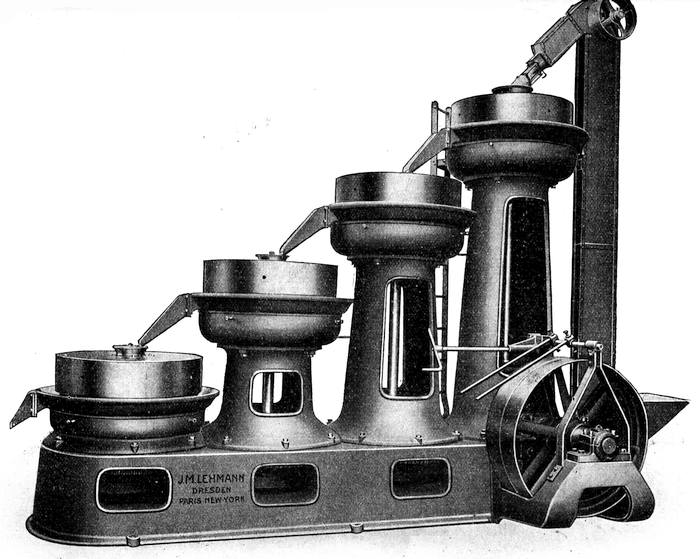
Fig. 24 c.
But side by side with the appreciation which these mills met
with, there arose a corresponding increase in the demands made on
them, such as the utmost nicety, greatest possible output, and least
possible necessity of after-heating, and these have been successively
answered by twin, triple and at the present time even quadruple
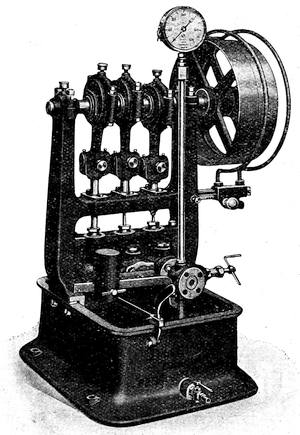
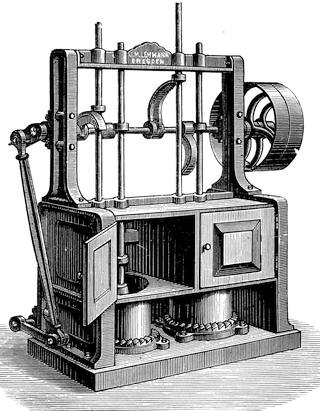
mills. fig. 23 shows a simple grinding mill which can only come into
consideration in connection with the smallest of branches, whilst
Fig. 24 a and b illustrates another with three successive stones arranged
one above the other, such as will be found in all the larger factories
of to-day. Also a triple mill but with grindstones of increasing
size pictured in fig. 24 c. A mill possessing four pairs of grinding
stones is given in fig. 25, and is calculated to meet each and every
conceivable demand.
Whilst simple, double and triple mills are brought on the
market in different sizes, corresponding to the outputs required, these
quadruple mills are only constructed in the largest sizes. They grind
perfectly, and without detriment to the flavour, deliver quantities
of cacao figuring at from 1000 to 1200 kilos daily. There is naturally
a larger output if the fatty contents of the cacao are considerable, a
thorough roasting being always presupposed.
The axles occurring on these quadruple grinding mills are
connected with one another by means of spur-wheels, and the axles
themselves run in ball-bearings, which not only permits a perfectly
noiseless operation of the machine, but also makes the action very
easy, that is to say, dependent on only very little motor power.
The cacao is raised to the hopper by means of an elevator, where the
quantity introduced into the machine is regulated, and then passes
between crushers occurring in the middle of the first pair of grinding
stones, which it subsequently leaves as a pasty mass. It is then
conducted along a groove into the second mill, and here undergoes
further grinding, and so to the third and fourth, where the process
can be described as trituration, for the cacao leaves the machine
in liquid form. Only in this manner is it possible to obtain the finest
ground product, without any disastrous accompaniment of excessive
heating.
Cacao mills with one stone suffice for the production of chocolate
mass on a small scale, but for the manufacture of cocoa powder,
twin or triple grinders must be employed.
All these are of the “Over-runner” type, act by their own
weight, and consequently do not involve the disastrous consequences
which were entailed by the “Under-runners” tried formerly.
About the middle of the nineties of the last century, experiments
were made with a view to superseding these types with mills having
stones of varying sizes, and first larger upper stones of a grinding
pair were tried, then larger under stones, but neither have been able
to maintain themselves in the workshop, and the grinders of equal
size still hold good as the fittest and most popular.
Fig. 25.
Attempts have recently been made to introduce a machine
combining mill and roller. Its value lies in the fact that with a relative
increase in the grinding rapidity, it does not involve a greater than
requisite heat, and on emerging from the machine the cacao shows
no deficiencies as to flavour, and is withal much finer than that
produced in other processes.
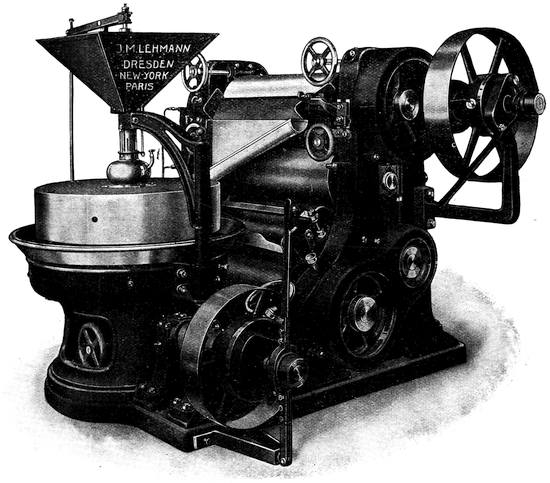
Fig. 26.
Fig. 26 shows such a machine. The mill on this serves merely to
reduce the hard kernel to a pulp, and this admits of the grinding
stones being placed farther apart, and so occasions no heat. Trituration
is then effected by a roller apparatus, for which operation
machines with four rollers have been proved most satisfactory. As
such roller machines are furnished with water-cooling systems, it
is possible for the cacao to be kept cool even on these.
6. Mixture with sugar and spices.
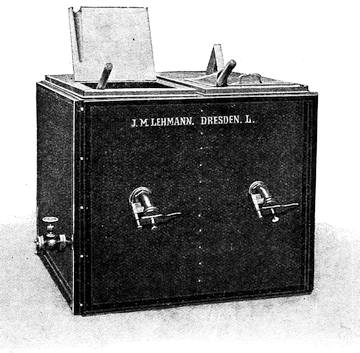
Fig. 27.
A thorough mixing with sugar can only be effected when the
cacao paste is heated to a temperature rather above the melting
point of cacao butter, that is to say, as high as from 35° to 40° C.,
and consequently the incorporating machine in which that operation
is carried on is provided with a steam jacket. For this process it is
advisable to have the chocolate in a semi-liquid condition, wherefore
the ground cacao issuing from the mills is transferred to steam-heated
vessels (fig. 27) fitted with taps suitable for drawing off the
mass as it is required. Formerly the cacao mass was fed into the
melangeur in lumps and there liquefied. But as this necessitated the
application of heat to the melangeur, attended with the risk of
cracking its under-plating, and also a postponement of the mixing
processes, whereby considerable time was lost, this method no
longer obtains to-day. It is at present usual not only to warm the
cacao mass beforehand, but the sugar also, by storing it in warm
chambers, so that the whole paste possesses a uniform temperature,
lowering of temperature in the melangeur is avoided, and there is
consequently no waste of the heating steam.
In some large factories the actual incorporation of cacao and
sugar is preceded by a preliminary mixing of large quantities, which
considerably relieves the strain on the melangeur, whilst it keeps the
machine rooms as far as possible free from superfluous dust.
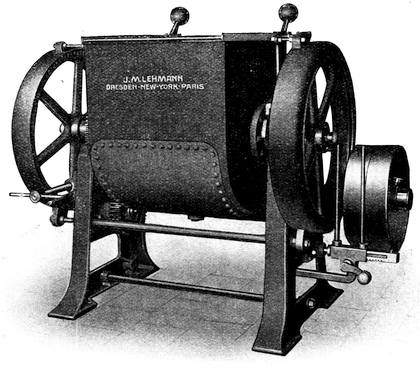
Fig. 28.
The mixing machine shown in fig. 28 can here be used with
advantage. As will be seen on comparing the illustration, it is provided
with a shifting trough. Such a machine, when closed down,
is capable of mixing from 100-500 kilos of chocolate. The mixing
is effected by means of two suitably shaped blades, and the heating
by a steam jacket. After the operation is completed, the mixed
material is turned out into portable troughs, and after having been
kept in a warm chamber for some length of time, transferred to the
melangeur for further treatment.
It has been found advantageous to keep the chocolate mass
so obtained in suitable receptacles for several days114, at a temperature
of not less than 20° C. and between that figure and 40° C.
So the sugar is enabled to penetrate the entire mass, which now
proceeds to the rolling processes carried out in the melangeur and
rolling machines. Shortly before its discharge from the latter, it
is mixed with spices, vanillin, eatherial oils and so forth.
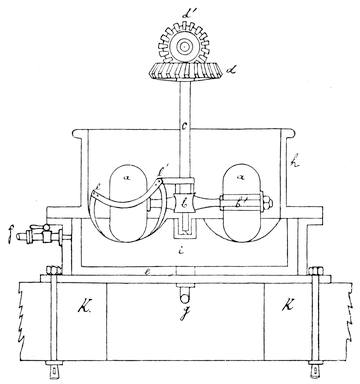
Fig. 29.
7. Treatment of the Mixture.
a) Trituration.
In describing the mixing machines, we do not intend to enter
into details regarding the machines formerly in use, but merely to
give a brief outline of the principles illustrated in their construction.
Trituration was formerly produced;
1. by rollers running backwards and forwards on a grinder;
2. by several cones rotating in a circle on a disc-shaped bed;
3. by means of rotating stones running in a trough;
4. by means of several cylindrical rollers;
5. by means of grooved cone moving in a grooved casing.115
At the present time only the type mentioned under 1. and 4.
are in general use. 3. is met with less frequently, and will be
described at greater length in a subsequent paragraph.
The machines 1. and 3. are put into operation prior to the
cylinder rolling mills, which finish off the incorporation of chocolate
and sugar and the levigation process only begun in the first-named.
The machines constructed in the manner described under 3.,
to which we now turn, were introduced by G. Hermann of Paris,
but are at present almost obsolete. Since they have some historical
interest and are typical of the development of the melangeur, we
annex a rough sketch showing their general construction in fig. 29.
The ellipsoid runners a made of granite work in the trough i
which is also of granite and is fitted with the casing h. The runners
rotate on their axles b so as to move in a circle. The two arms of
the axis b have at the centre an elliptical ring with a quadrangular
opening, into which fits the similar shaped part of the vertical shaft c
fitted with the toothed wheels, d and d′, which are set in motion by
power transmitted to the shaft and its connections. The arm b has
some play downwards, so that it can adjust itself vertically according
to the greater or less quantity of material in the mill. The two
steel blades, e and e′, are shaped to fit the cavity of the trough; being
connected with the shaft c they revolve with it and sweep down
the cacao mass adhering to the sides of the mill. Between the
foundation k and the trough i there is a space l into which steam
can be introduced through f, the condensed water passing away by g.
All machines of this kind have now been displaced by the
melangeur which is capable of turning out a much larger quantity
of material with a relatively smaller expenditure of power. The
operation of mixing chocolate is not a mere mixing, for the
pressure exerted by the runners is also an indispensable factor.
On that account the ordinary mixing machines have not proved
serviceable, especially in the case of chocolates containing a small
amount of fat, such as the cheaper kinds, while the addition of cacao
butter to facilitate the working of the machine would considerably
increase the cost of production. Melangeurs are generally constructed
on the same principle as the edge runner grinding mills
which are so much used; but they differ from them in so far as the
bed-stone revolves, while the runners merely rotate on their axles
without revolving.
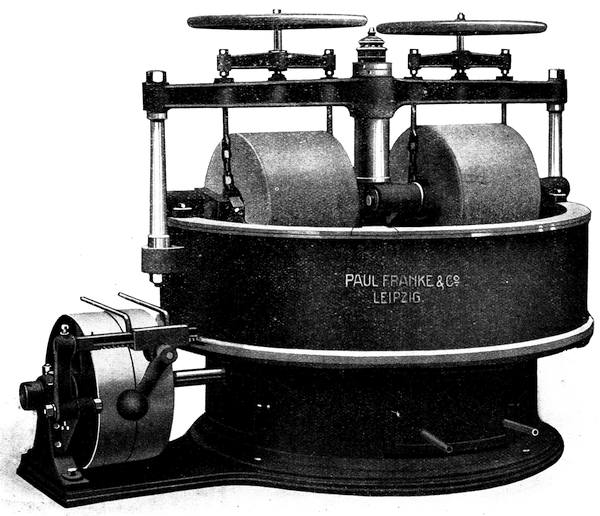
Fig. 30.
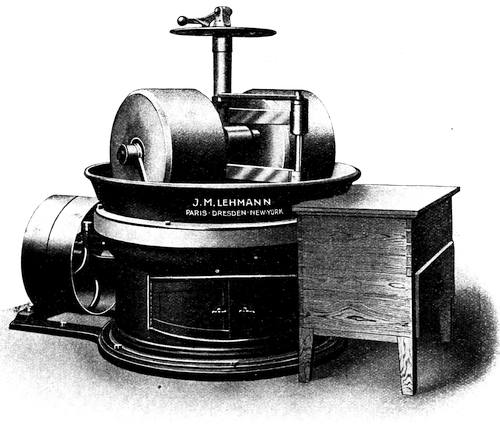
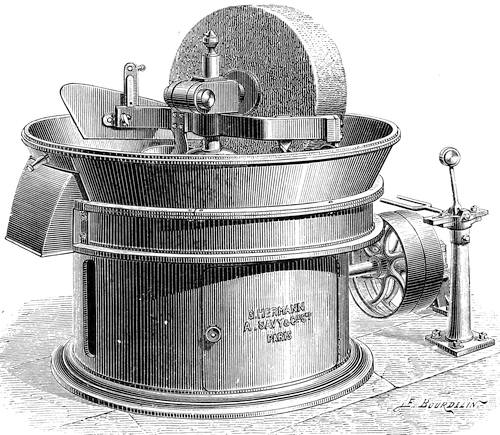
The melangeur with travelling bed-stone, as constructed by
Lehmann, is shown at fig. 30; it is fitted with an arrangement for
lifting out the runners.
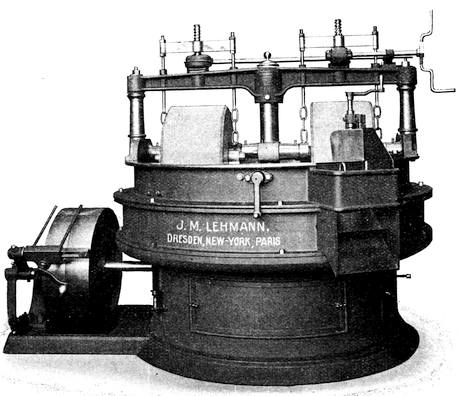
Fig. 31.
The bed-stone as well as the runners are made of granite.
Each runner has an axis working in plummer blocks, so that it can be
lifted out independently of the other one. By that construction the
runners are prevented from taking an oblique position as was the
case with the mills formerly made, since one runner would be
forced downwards or tilted on its outer edge whenever the other
one was raised up somewhat. The bed-stone of this machine revolves
and it is easily heated by steam pipes from below. One important
advantage of this machine is that being low it can be very easily
charged and emptied. The contrivance for lifting out the runners
prevents them thumping upon the bed-stone that might otherwise
readily happen when starting the machine, and it also lessens the
wear of the driving bands; moreover, large lumps of sugar or cacao
are very readily crushed down and, so, the working is much facilitated.
The emptying of the melangeur is readily and safely effected,
while the bed stone is revolving, by holding a shovel so that the
cacao is thrown up against the shovel. A melangeur of this construction
is represented by fig. 31; it has three runners and underneath
the bed-stone is fitted a steam engine which supplies driving power,
the exhaust steam being used for heating the machine.
Although this emptying by hand is not attended with any
serious drawbacks, yet it involves loss of time and is rather inconvenient,
so that the demand for mechanical automatism in this
operation was very considerable. It is now some years since Messrs.
J. M. Lehmann patented an apparatus for the mechanical discharging
of the chocolate mass from these machines, but their invention still
holds good. A melangeur provided with such apparatus is shown
on fig. 31. Here a vertically moving shovel is sunk behind the
outlet, gradually damming the material, and causing it to rise above
the edge of the tank and fall through the opening. A second but
horizontally working arrangement, which in this case as in the last
is controllable by means of a crank, conducts the remainder of the
material to the same shovel. So the material is discharged within a
few minutes.—These melangeurs are built for varying outputs.
Fig. 32 illustrates one of the largest yet constructed. Its base has a
diameter of 2 metres, and the machine itself has a capacity of 5 cwts.
To avoid the mixing of dust with the sugar as far as possible, the
whole melangeur is provided with a dust-proof protector.
b) Levigation.
An extreme fineness and homogeneity of the chocolate mass
is obtained in the employment of cylindrical rolling machines, for
the construction of which we are indebted to G. Hermann of Paris.
Every kind of chocolate must be passed through the rolling machine
at least once or twice even when finely powdered sugar is used,
though in this case it is less a question of sub-division than of incorporation
and intermixture. The best qualities are passed through the
machine from six to eight times, or even more. The mass is finally
fed into the machine in cold blocks and so ground off. Granite is
the material chiefly employed in making the rollers, although it is
not every variety which can be adapted to this purpose. Apart
from the fact that granite, or indeed any other mineral stone, seldom
occurs in compact masses and free from flaws, neither porphyry
nor the stone generally described as granite is suitable for employment
in the construction of mill rollers. A kind is generally preferred
which intermediates between granite and porphyry as to hardness
and possesses excellent grinding capacities, and which goes by the
name of diorite. No other stone can compare with this diorite in
respect to the above qualities, and the chief firms engaged in the
construction of roller machines possess their own quarries. But we
shall return to this later, for recently experiments with case-hardened
casting rollers (Krupp steel) and hard porcelain have yielded very
flattering results.
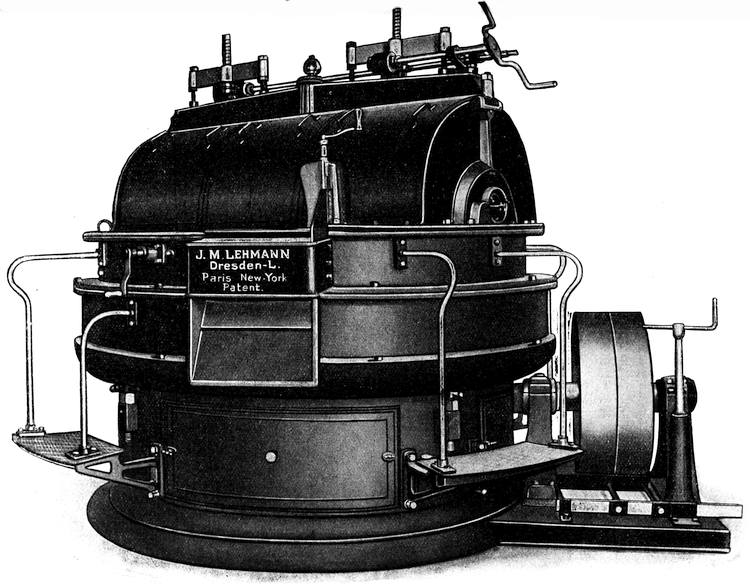
Fig. 32.
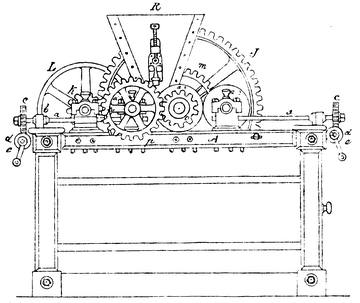
Fig. 33 a.
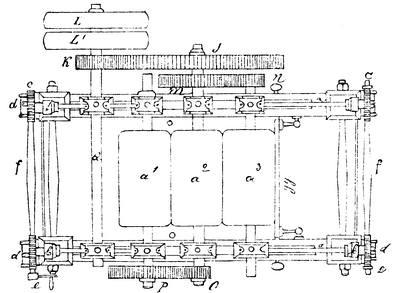
Fig. 33 b.
We shall now enter into more detail respecting the principle
illustrated by these rolling machines. The plasticity of the chocolate
mass necessitates a rotation of the cylinder surfaces in opposite directions
with dissimilar velocities. Accordingly two or more rollers are
caused to work against each other, and in compliance with this principle
of sub-division with differential velocities, their axles are fitted
with wheels, of which each has a different number of cogs.
So those rollers furnished with the greater number of teeth
revolve more slowly, whilst in opposite instances there is a corresponding
acceleration.
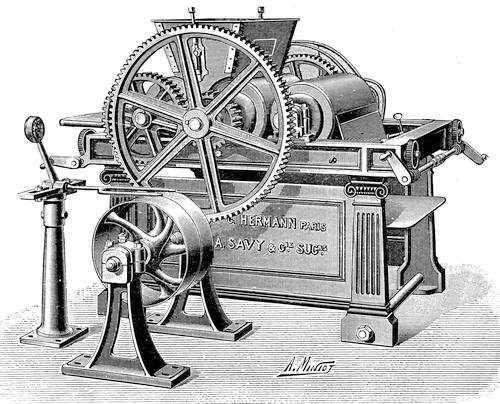
Fig. 34.
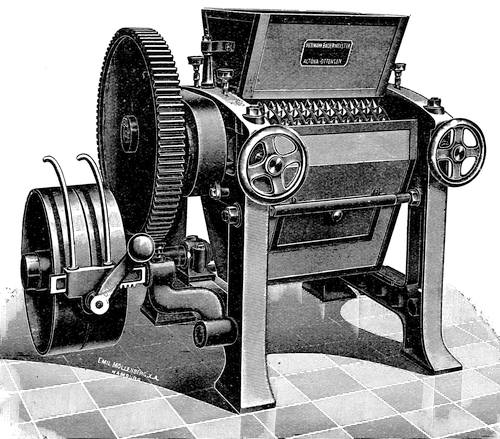
The construction of the machines now in use differs more or
less from that of the type first invented by Hermann, plan and elevation
of which appear in figs. 33 a and 33 b respectively.116
The granite rollers at a1, a2, a3 are fitted with an octagonal
iron axle that is somewhat thicker at the interior part and they are
mounted upon a frame as shown in the drawing. The sockets of the
central rollers a2 are fixed and each one is held in position by three sets
screws; those of the two other rollers can be shifted along grooves
in the frame and when the cylinders a1 and a3 have been brought
into proper position relatively to the cylinder a2 they are held fast
by the set screws p.
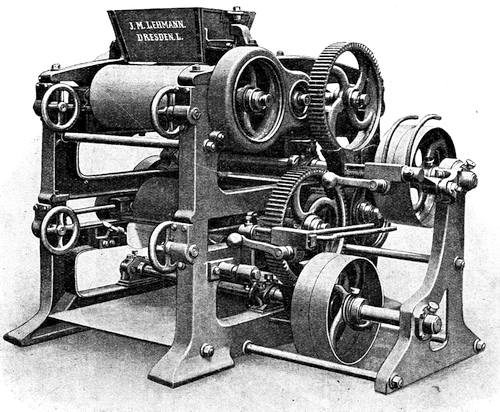
Fig. 35.
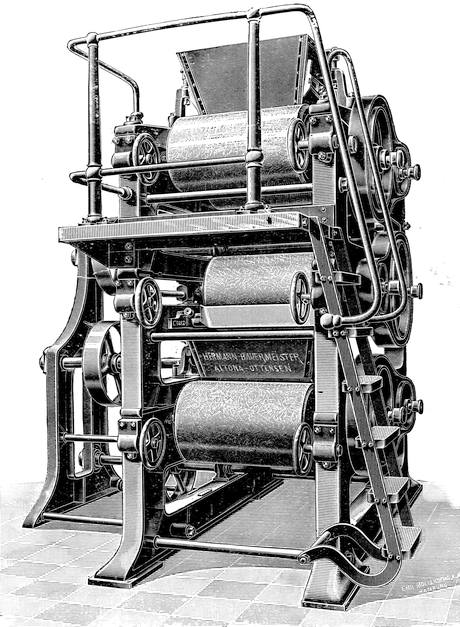
Fig. 36.
For the purpose of this adjustment, there is at each end of
the machine a horizontal wrought iron shaft f that can be turned
by the winch e, and these shafts are fitted with two endless screws d
working in the corresponding wheels c. These occur on the spindles
a, which screw in and out of the bearing blocks of the rollers a1
and a2, but turn only in the fixed collars b without being shifted
from their place. The result is that on turning the cranks e the
corresponding cylinder a1 or a3 is moved nearer to, or further from,
the central cylinder a2, while the position of all of them always
remains parallel. The shaft Q is set in motion by the driving wheel
L fitted with the loose wheel L1. It acts first upon the cog wheel K
which works in the larger wheel J on the axle of the central roller a2.
That works in the cog wheel O and the wheel P fitted to the roller a1
driving them as well as the wheel M and the pinion N of the roller a3
The result is that the axle a2 makes 1¾ revolutions and a3 6-1/8 revolutions
while a1 in the same time makes only one revolution.
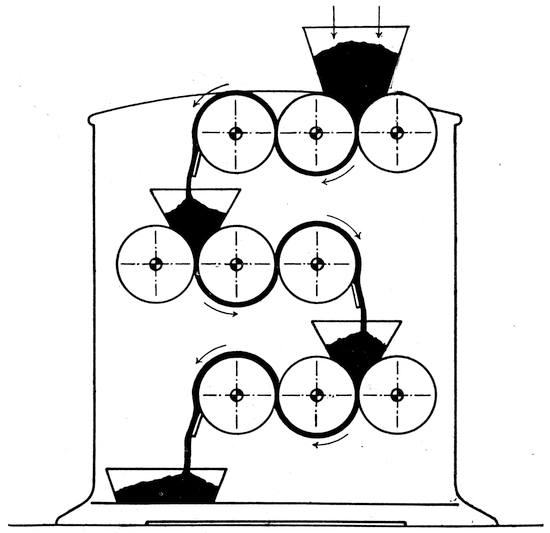
Fig. 37.
The cacao or chocolate is supplied to this machine by the
hopper R which is placed between the rollers a1 and a2. The pasty
mass adhering to the rollers is carried forward by the quicker moving
roller a2 and it is ground finer between the rollers a2 and a3, after
which the material is removed from a3 at the outer side by an
adjustable blade gg and then falls down into a receptacle below.
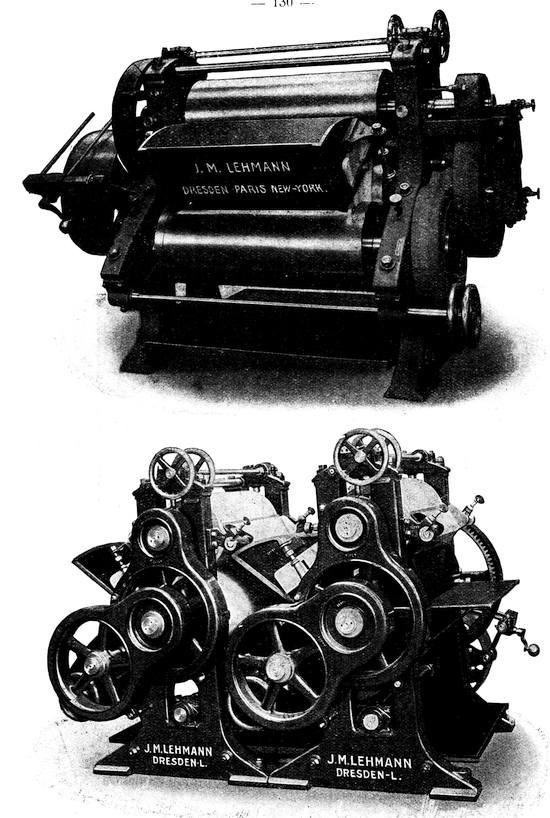
Figs. 38 and 39.
On the design fig. 3434 we see a machine of more modern construction
ready mounted. The receptacle parts of the same are arranged
and connected in full agreement with the above mentioned except
that the motion is effected by the driving power fitted to the machine
on the ground on the left side.
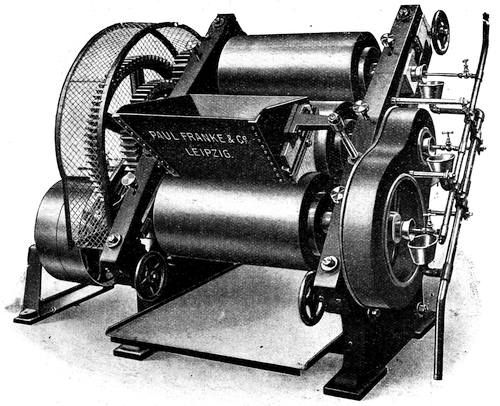
Fig. 40.
The principle of this roller machine has long been applied in
the building of other types, and we find that these, variously altered,
renovated and improved, are to-day an indispensable equipment in
every chocolate factory. In the following pages we give a
description of some of the best-known constructions of refiner.
The so called battery rolling mills constitute a remarkable
innovation. It is apparent that the more rollers a cylinder machine
contains, and the greater their length and diameter, all the more
efficacious will the working of the machine be. Batteries have
accordingly been constructed, whereby two, three or more roller
systems are combined, one to every three rollers, and rising one
above the other, so that they slant upwards much as shown in Fig. 40.
As the battery rolling mills possessed the disadvantages that
they took up too much room and could not be well fed and regulated,
they are generally replaced by rolling machines of from 6 to 9 rollers,
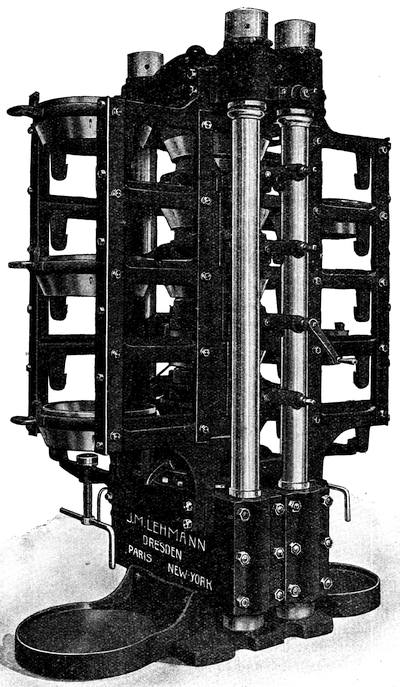
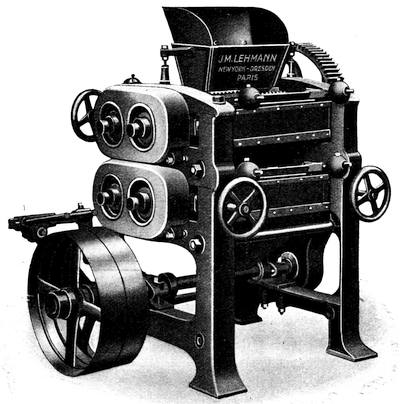
first constructed by J. M. Lehmann. These rolling machines of 6 to
9 rollers which we see before us in Figs. 3535 and 3636 are really systems
of 3 rollers fitted one over the other. They therefore take up the
room of a 3-roller machine and are quite as easy to work.
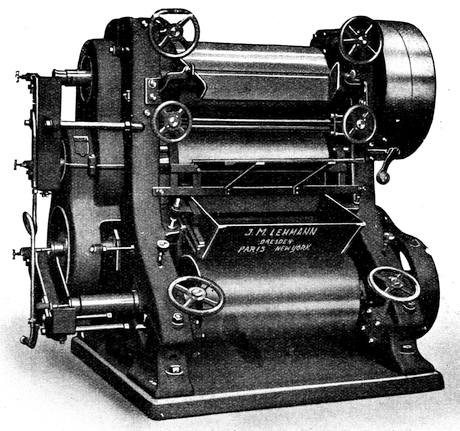
Fig. 41 a.
As will be seen from the design of a nine-roller apparatus,
fig. 37, the chocolate mass descends from one roller system to the
other, and is fine rolled in a third of the time otherwise required,
and at one operation, with corresponding saving of labour. The nine
roller apparatus are provided with landing stage and steps, and fed
either by means of elevators, or from above.
Fig. 38 shows a recent construction, three roller apparatus
(case castings, cf. below) standing vertically, which accordingly takes
up little room. The hopper is low-lying, whilst the discharging is
effected from the upper roller, and accordingly admits of the
occasional use of a somewhat larger size of transport trolley. This
type also occurs with 6-9-12 rollers, as apparent from fig. 39.
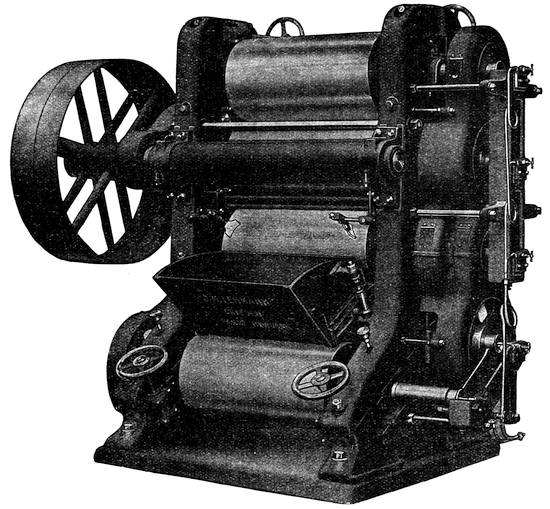
Fig. 41 b.
Whilst these systems were exclusively supplied with rollers
made of granite or hard porcelain up to a few years ago, it has been
found that good results are obtained by the use of cast rollers, and
they have been for some time employed on machines of three, four
and five rollers. (Figs. 38, 40, 41 a-c.) In consequence of the non-porous
surface of these steel rollers, it is possible to grind to a finest powder,
merely in one operation, without passing the chocolate through the machine
several times; and the so-called “Burning” of masses which have
not been properly mixed cannot arise in this case, though it is true
that the apparatus must be provided with water cooling arrangements
to avoid a too excessive heat. They are specially adapted to the preparation
of the more ordinary qualities, and are even occasionally
employed for finer chocolates, for obviously these must be again
submitted to a rolling process, when granite or porcelain rollers are
preferred.
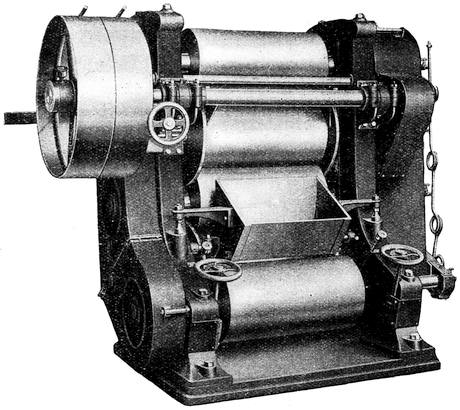
Fig. 41 c.
For this reason the 6, 9 or even 12 roller mills have been more
discarded since the last grinding process has been performed by granite
rollers (cold process).
In order to avoid the disadvantages of the pulley drive, it is
in certain cases advisable to drive each machine direct from an
electric motor. Fig. 42 illustrates a refining machine driven in this
manner.
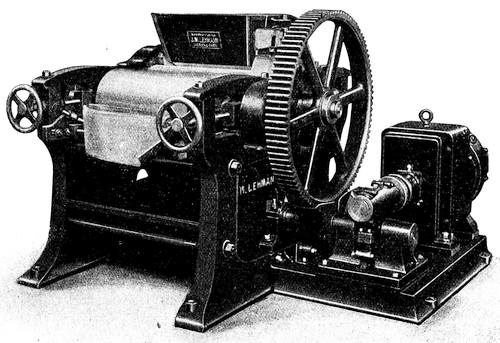
Fig. 42.
c) Proportions for mixing cacao mass, sugar and
spices.
The relative proportions of cacao, sugar, and spices, as well
as of starch as in the manufacture of the cheaper sorts, vary considerably.
Generally speaking 50 or 60 parts of sugar are added for
50 or 40 parts of cacao mass; the following are a few formulae
applicable for the production of those kinds of pure chocolate that
are most used.
| A. Hygienic chocolate. |
| Cacao mass |
} equal parts of each. |
| Powdered sugar |
| B. Spiced chocolate. |
| a) |
|
b) |
| Cacao mass |
4 kg |
|
Cacao mass |
4 kg |
| Sugar |
6 kg |
|
Sugar |
6 kg |
| Cinnamon |
72 g |
|
Cinnamon |
130 g |
| Cloves |
38 g |
|
Coriander |
8 g |
| Cardamoms |
16 g |
|
Cloves |
88 g |
|
Oil of lemons |
2 g |
|
Cardamoms |
16 g |
| c) |
|
d) |
| Cacao mass |
5 kg |
|
Cacao mass |
5 kg |
| Sugar |
5 kg |
|
Sugar |
5 kg |
| Cloves |
80 g |
|
Cinnamon |
100 g |
| Cinnamon |
220 g |
|
Vanilla |
100 g |
| Mace |
8 g |
|
or Vanillin |
2·5 g |
|
Mace |
2 g |
|
Cardamoms |
4·2 g |
| e) Spanish spiced chocolate. |
| Cacao mass |
5 kg |
|
Cardamoms |
82 g |
| Sugar |
5 kg |
|
Mace |
44 g |
| Cinnamon |
116 g |
|
Vanilla |
40 g |
| Cloves |
50 g |
|
or Vanillin |
1 g |
|
Oil of lemons |
1 g |
| C. Vanilla chocolates. |
| a) |
| Cacao mass |
5 kg |
| Sugar |
5 kg |
| Cinnamon |
160 g |
| Vanilla |
50 g |
| (or Vanillin |
1·2 g) |
| b) |
|
c) |
| Cacao mass |
4½ kg |
|
Cacao mass |
4 kg |
| Sugar |
5½ kg |
|
Sugar |
6 kg |
| Cinnamon |
150 g |
|
Cinnamon |
120 g |
| Vanillin |
1·5 g |
|
Cloves |
20 g |
|
Vanillin |
1·6 g |
The powdered spices as given above may be replaced by
corresponding essential oils, but see page 237 for remarks on
this point.
If the chocolates made from beans rich in oil contain too much
fat to mould properly, a small percentage of their constituent cacao
mass can be replaced by cocoa powder made from the same kind
of bean, but defatted, in the case of the finer qualities; and when
inferior varieties are under consideration, the same result may be
attained by a sufficient increase in the proportion of their other constituent,
sugar, as e. g. 55-60 parts of to 45 or 40 parts of cacao mass,
so disturbing the usual equality of the two ingredients mixed together.
Very cheap chocolates in particular are prepared from a smaller
percentage of cacao mass and show a corresponding increase in their
sugar content. But if the sugar exceeds 65 percent, it is no longer
possible to mould these chocolates, and the addition of fresh cacao
butter becomes a necessary preliminary to this operation, cf. also
the first part in section IV. Such varieties would have a composition
somewhat like the following:
| Cacao mass |
25 |
parts |
| Sugar |
67 |
" |
| Cacao butter |
7 |
" |
| Spices and vanillin as above |
1 |
" |
In the experimental preparation of samples of chocolate mass it is
not advisable to employ large quantities of ingredients, when a waste
of material is bound to ensue, but to begin with mixing small quantities
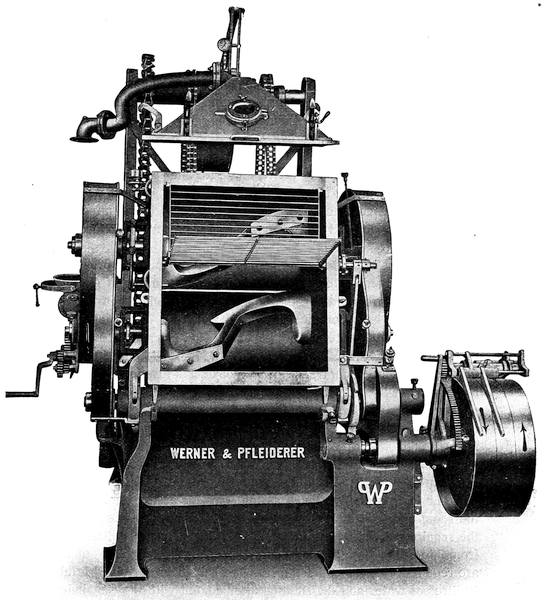
of one or two kilos. The small Universal Kneading and Mixing
Machines, Patent Werner & Pfleiderer, Type 1, Class BS, can here
be used with advantage. They are specially intended for small
outputs and experimental work; but we shall return to their description
later, after stating that they are furnished with heating
apparatus, stuffing boxes and air-tight lid, and can easily be taken to
pieces, greatly facilitating the removing of the mass.
8. Manufacture of “Chocolats Fondants
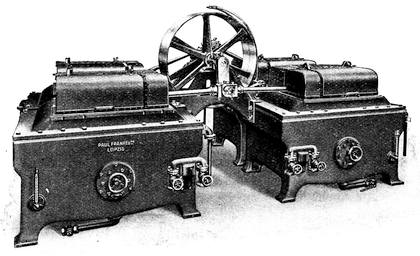
Fig. 43.
Recently the creams sometimes described as in the heading
have enjoyed a vast popularity, and are sold as eatable chocolates in
ever-increasing quantities. As far as can be ascertained, they were
first manufactured in Switzerland, melt readily, and have a correspondingly
large amount of fat, resulting from the addition of cacao butter,
which distinguishes them from ordinary chocolates. When readily
melting chocolates were first introduced, it was a prevailing opinion
that the required property could only be obtained by increasing the
amount of fatty content. Now the excessive evidence of fat in
chocolates is very objectionable, both as regards taste and digestibility.
To avoid this, therefore, the chocolates are treated mechanically,
to attain the required character of readily melting. The machines
used for that purpose are termed “Conches”, because the trough, in
which the chocolate is rubbed into a long cylinder, has somewhat the
shape of a long shell. For the working up of chocolates in conches,
the necessary conditions are;
1. that the chocolate should have been ground perfectly fine,
2. it must contain such an amount of fat as to become glucose
on warming, not indeed so thin as that used as coating
material, but nevertheless softer than the ordinary cake-chocolate
of good quality.
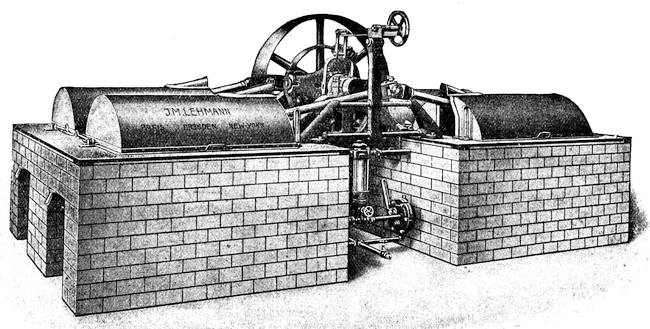
Fig. 43 a.
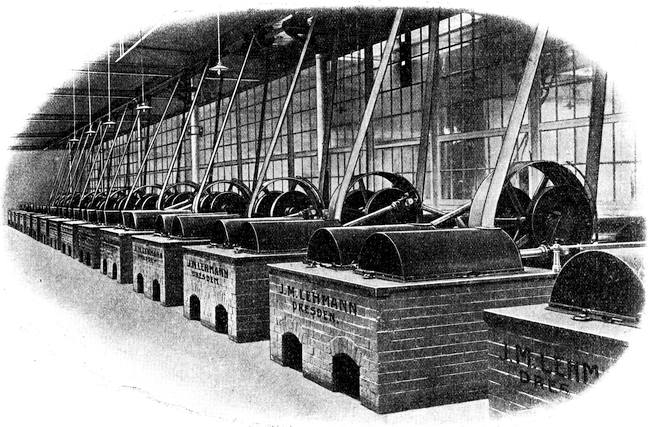
Fig. 44.
The machine can be heated by means of steam, hot water
pipes, gas or charcoal stoking, according as they are available in
the place of installation, and the temperature should rise above
70-80° C. for fondants, and 50° C. for milk chocolates. In factories
with water power or electricity, continuous fondant machines can
be worked day and night, but when only worked during the day,
must be kept warm overnight. Constant tending of the machine is
unnecessary, as it works automatically. After a treatment of from
40-48 hours, the chocolate attains the requisite character (i.e. it melts
readily), and a rounding off of taste, which are the properties of all
good brands. Milk chocolates can also be advantageously prepared
in the conche, as also covering or coating cacaos of all kinds, which
harden considerably in consequence of this treatment.
Figs. 43 and 43 a show quadruple conches of the modern
type with hot water, wherein four troughs are arranged in pairs,
and one opposite the other. Conches with only 1 and 2 troughs
are also constructed, and in various sizes, the troughs sometimes
having a capacity of 125 and 200 kilos, so that the quadruple
conche is capable of holding five or eight hundred kilograms
in all. The curved bottom of the troughs, as well as the rollers
fitted in them, are made of granite, and the front wall
strongly bent in at the corner, so that the mass is forced over
the border of the front wall, where there are openings for its
discharge as well. To prevent radiation as far as possible, it is
best that the troughs be walled in, the troughs are either walled.
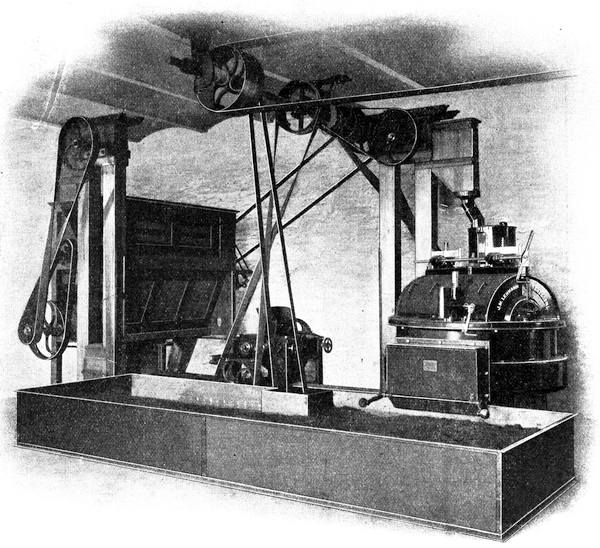
Fig. 44 shows the room of a modern chocolate factory, with
15 conches.
“Chocolats fondants” are from a gastronomic point of view,
the finest chocolate product on the market, and it is not remarkable
that this branch of the chocolate manufacture has witnessed a considerable
extension, and is likely to extend still more.
9. Heating chambers and closets.
The manufacture of chocolate has been very considerably
facilitated by the introduction of heating chambers and closets, which
have now become an indispensable feature of every factory in the
industry. In these chambers the chocolate which has still to be
rolled, as well as that already submitted to this operation, is stored
and kept at a temperature of 60° C. until it can be further treated
(moulded). This manner of heating involves an appreciable cheapening
of the production, for masses which are dry and apparently require
an addition of fat recover in such a manner during a twenty
four hours’ storing in the heating chambers that such addition becomes
unnecessary. But especially when chill casting rollers are employed,
which the mass leaves in a very dry state, the use of these heating
chambers is indispensable. They should be available in every factory
to such an extent as to find room for the total output of one day,
though even twice or three times this amount might very well be
provided for. Closets heated by steam are best adapted for small
factories, such as are illustrated in Fig. 45. They possess double
doors, are walled in, and are capable of holding from 300-400 kilos
of chocolate mass for each metre of length. Larger factories should
furnish themselves with chambers, which are more open to access and
on the walls of which iron shelves can be introduced, heated by
steam pipes arranged underneath. A typical chamber, measuring 2·8
metres in breadth (including passage) and 5 metres in length would
hold about 2,500 kg of chocolate.
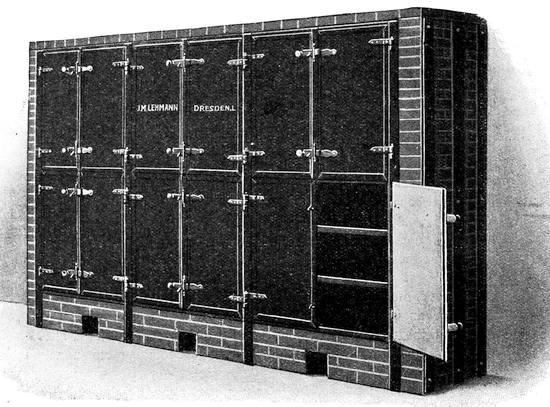
Fig. 45.
10. Removal of Air and Division.
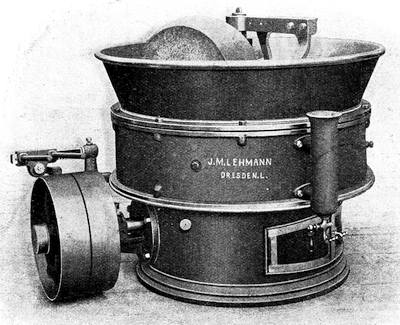
Fig. 46.
After emerging from the final rolling process, the chocolate is
stored up in heating chambers until it is ready to succeed to the
moulding, prior to which, however, it must be freed from air and cut
up into small portions. Until recently, it usually came next in a
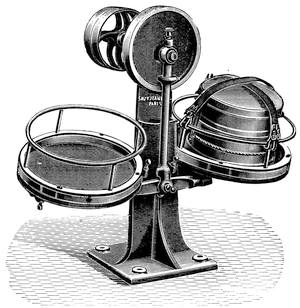
melangeur provided with a dish-shaped bed-stone made of granite,
as illustrated in fig. 46, where it was kneaded and reduced to a uniform
plasticity and heated to the temperature required for moulding.
The melangeurs devoted to this purpose are now superseded by special
tempering machines.
A machine of this recent construction, used for working solid
and semi-liquid material, is shown in fig. 47. The tank intended as
a receptacle for the chocolate mass is in this case made of iron
and, to facilitate cleaning, smooth in the interior. It runs in a
water-bath, the supply in which can be controlled by steam or cold
water. The granite runner is provided with a lifting device, admitting
of the working up of material containing foreign ingredients
like nuts, whole and fine-split.
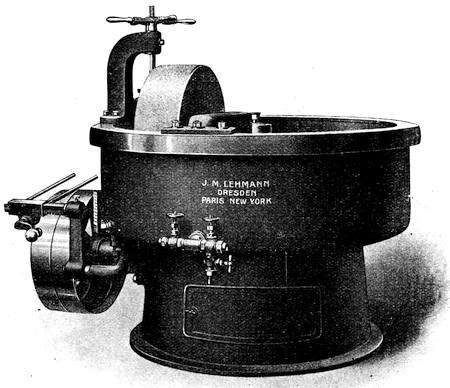
Fig. 47.
The mass is taken out of the machine in lumps, and in order that
it may be reduced to a temperature suitable for the removal of air
(about 26-32 ° C. on the outside) it is laid to cool on wooden, marble
or iron tables. When this temperature is arrived at, large lumps of
chocolate are introduced either into the air-extracting or the dividing
machines.
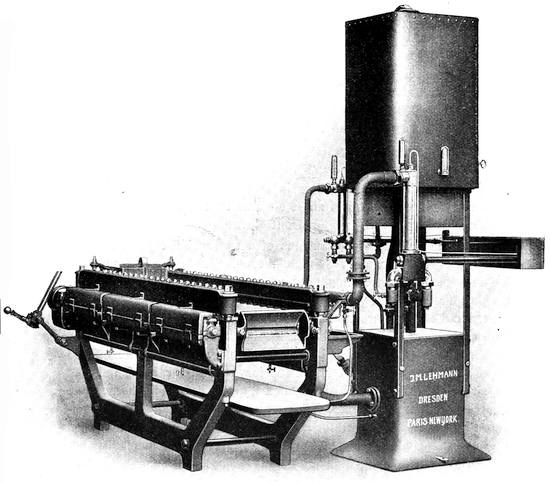
Fig. 48.
After the importance of the tempering processes had at length
been recognised, inasmuch as the maintenance of the temperature
prescribed is of immense influence on the chocolate subsequently
produced, and it had on the other hand been ascertained that such
machines as described above could not be absolutely relied upon,
for the shaking tables involve an occasional excess of tempering,
the idea of a machine which should completely and automatically
perform this task was finally conceived. This new machine, given
in fig. 48, and already differing from all other tempering machines
in external appearance, ushers in an entirely fresh process respecting
the modus operandi prevailing in the present manufacture of
chocolate, which does not fail to satisfy the highest expectations.
It may be said to work continuously, for no matter what the temperature
of chocolate passing into it may be, the material leaves the
machine at the temperature desired within a lapse of one minute.
According as more or less chocolate has to be turned over in the
moulding department, the machine can be stopped or set in motion
without detriment to its efficacy. Besides this, it cleans almost automatically,
so that a quick change of quality is always possible. The
special virtue of this machine is that it turns out the material with
such a degree of homogeneity as has never before been known,
making moulding at much higher temperatures a possibility. There
is yet another side issue, namely a doubling of the life of the moulds,
and finally, owing to the fact that the often considerable amount of
waste material is done away with in this process, the moulding shop
is spared to some extent. The series of rollers through which the
chocolate passes is maintained at a proper temperature by means
of automatic water apparatus. The daily output of the machine figures
at 3000-4000 kilograms. The material is passed on out of this
machine to the dividing and moulding processes.
The necessary extraction of air follows immediately on
the tempering process, for the blades of the scraper then release the
chocolate mass from the rollers in thin layers, between which air
penetrates. The removal of air is effected by machines, an old type
of which is shown in fig. 49 (in front elevation).
It can be warmed by means of a charcoal fire placed in the
space i, or by any other suitable means. The chocolate mass is
fed into the cylindrical hopper a, at the base of which occurs an
archimedian screw b, which is propelled by the shaft and cog-wheel
system c d e in the direction indicated by the arrow. Thus the chocolate
mass is forced into the box f, leaving which in cylindrical form,
it succeeds to the travelling band h. It is now almost entirely freed
from air. As the material is pushed forward on the band, it is cut
off either by a knife g fixed to the box f, or divided as far as possible
into equal parts by a double knife with adjustable blades corresponding
to the weight required for a chocolate square. This manipulation
presupposes a fair amount of skill on the part of the machinist, but
this once attained, the division ensues as precisely and simply as
can be desired.
Air-extracting machines of recent construction, although still
partially built on the above principle, are at the same time generally
developed as automatic dividing machines.
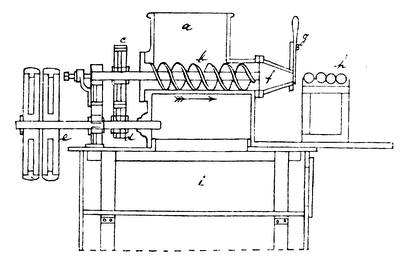
Fig. 49.
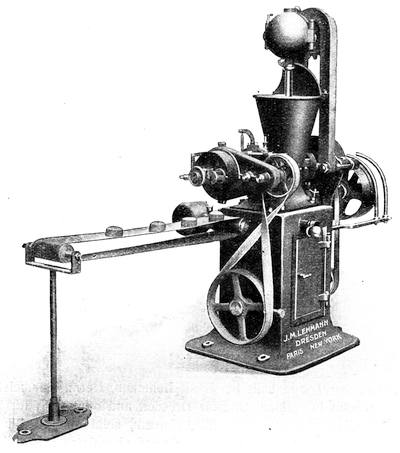
Fig. 50.
Fig. 50 shows such a machine for solid and semi-liquid chocolates.
By means of this, the material is next conducted along a vertical
screw path in even mass to the horizontal screw, and so a second
filling with the hand is rendered unnecessary. After it has been freed
from air in this, it enters a revolverlike cutter, which discharges the
divided portions on a travelling belt. On the latter it is conducted to
a table standing near, where it is laid into moulds. The machine is
of very strong make, and puts out from 15-250 gr, divided into
approximately 10-25000 squares, within a space of ten hours.
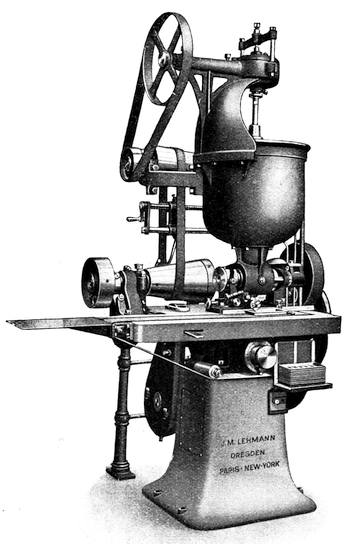
Fig. 51 a.
Figs. 51 a and b give finally two of the best known types
which have a very extensive application, protected by patent imperial
(Germany), and built by J. M. Lehmann, Herm. Baumeister,
J. S. Petzholdt in Döhlen, G, near Dresden and others. With this
patent dividing machine of J. M. Lehmann, solid and semi-liquid
chocolate material, as also nut and almond chocolates are divided
exactly, in any weight from 18 to 250 grammes, and then conducted
in strips of equal size to the mould previously mentioned. As far
as cleanliness, purity, and easy management are concerned, it fulfills
all the demands which can be expected of the most modern
machine.
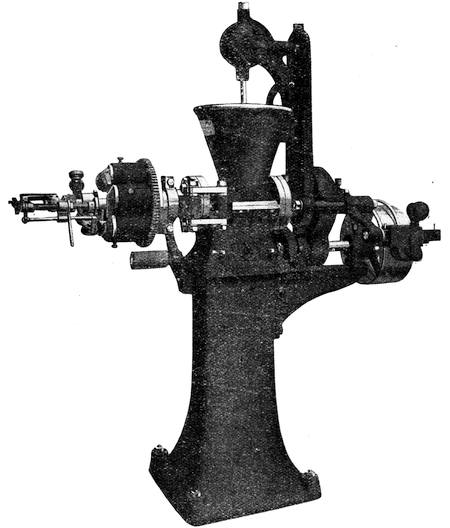
Fig. 51 b.
11. Transference to the Moulds.
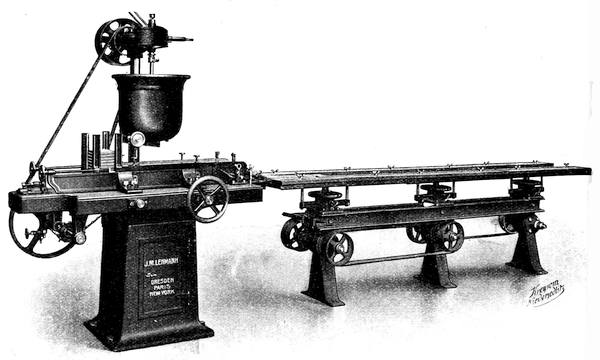
Fig. 52.
The pieces of chocolate, on emerging from the dividing processes,
are placed separately in iron moulds, that is to say, as far
as this has not already been done in the dividing machine. It is
important that these should have the same temperature as the chocolate
mass, in order to prevent the formation of spots on the surface
of the cakes, and to obtain a good and non-greyish fracture. The
temperature for moulding smaller objects can be fixed at between
27° and 32° C. and for the larger may be considerably lower. In
summer also, moulding may be proceeded with at a lower temperature
than in winter. According to a note in the Gordian (1895,
No. 4) the moulding may be carried out in summer, when the
atmospheric temperature is;
- from 25-31° C, at 26-27·5° C
- " 18·5-25° C, at 28·5-30° C
- " 12·5-18·5° C, at 31-32·5° C
In cold weather, the cakes may be moulded at a temperature of from
32·5-35° C., according to their thickness. When not manufactured
in the automatic machine shown in fig. 48, the mass should be
otherwise controlled as regards temperature, which should be
registered by a thermometer introduced therein. The moulds are
for the most part filled with plastic and liquid chocolates, and their
depths determined and modified by the weight of material which
they are destined to receive.
Fig. 52 shows a machine which conducts the semi-fluid mass
to the moulds in the following manner. The moulds are automatically
introduced under the apparatus, and filled from the small stirrer
above. They then succeed to the shaking table and are finally transported
to the cooling room. On this machine moulds of from
75-350 mm long and 75-225 mm broad can safely be employed.
There are two different forms in which chocolate is sold,
namely, that intended for domestic purposes, and that which is to
be consumed as an article of luxury. The kinds known as cake,
rock and roll chocolate belong to the first class, the several pieces
weighing 50, 100, 200, 250, 500 up to 5000 grammes. Tin-plate is the
only material of which moulds are made; and these generally have
a capacity rather greater than is necessary for holding the particular
quantities to be moulded. The chocolate is therefore, as described
above, divided into given weights, and generally deposited direct in
the moulds by the dividing machine. The divided portions of chocolate
are pressed down in the moulds by hand, equally distributed in
the latter, and then transferred in the moulds to the shaking table or
combination of shaking tables to be described later. On the shaking
table the soft chocolate soon penetrates completely into all the corners
and impressions of the stamped tin moulds. The removal of the
cooled cakes from the moulds is easily effected by pressing.
These moulds are generally provided with from four to ten
ridges or indentations, so that the chocolate can be conveniently
divided, and as required for use. Others again have a similar number
of compartments.
The compartments may be impressed with any kind of
inscription, so that such information as the name of a firm can always
be reproduced on the cakes.
Broken chocolate is generally of inferior quality, brought on
the market without any protective covering.
In those kinds of chocolate which are known as articles of
luxury a distinction is to be made between;
1. Those moulds which are in one piece and completely filled
with chocolate, so that the superfluous mass can be removed by a
knife. In such cases the weight of the cakes is exactly regulated by
the capacity of the moulds.
2. Those intended for moulding various figures of fruit etc.
in which two or three parts make a closed space which is of the
form desired.
Among the moulds of the first type must be numbered those
used in the preparation of small tablets and sticks, and the sweetmeats
known as Napolitains and Croquettes.
The second class comprises moulds for making chocolate cigars
and chocolate eggs, and also the double moulds.
The moulds for the smaller tablets, cream sticks, napolitains
and croquettes are also made exclusively from tin-plate, and the separate
parts are enclosed in a stout iron frame, the top of which is
ground down smooth, so that any superfluous portion of the filling
can easily be scraped away. In that way from six to thirty pieces
can be cast in one mould at the same time: the cooled chocolate can
be released from the moulds by gently tapping one corner against
a table. In napolitain moulds protecting hooks are attached, to avoid
their sustaining any injury in this operation.
Examples of the more frequent moulds.
1. Chocolate Cigars.
These are made either by introducing the chocolate mass between
the two halves of a double mould, of which each corresponds
to a half of the cigar shape to be moulded and which each fit exactly
one on the other; or else by pouring it into hollow moulds stamped
out of one complete piece. Moulding presses117 are utilised in
the manufacture of material en masse. In these the cigars are
filled into iron moulds, afterwards held together by means of iron
combs, and so introduced in to the press. For each size and shape
special moulds and plates are essential. Neither barium sulphate nor
zinc white may be employed to produce an imitation of the ash on
ordinary cigars, as both are objected to by health inspectors; nor
are they necessary, for in phosphate of lime (tricalcium carbonate)
we possess a perfectly harmless and at the same time efficient substitute,
when it is mixed up with starch syrup.
Other figures, such as fish etc., may also be produced in chocolate,
by means of the moulding press, when it is furnished with
stamped moulds, corresponding to the forms required.
2. Chocolate eggs.
These are generally made hollow, unless they are very small,
by pressing chocolate in two halves of an egg-shaped mould and
then uniting the two parts. Another method patented by Th. Berger
of Hamburg118 seems less practical. A mould is made of soft sheet
caoutchouc blown out; this is dipped into liquid chocolate and, after
the adhering coating has hardened, the air is let out of the mould.
The use of caoutchouc moulds would render this method too costly,
since the alternation of temperature soon makes the caoutchouc
unserviceable.
3. Various figures, fruits, animals, and other small
objects.
Double moulds are used for making these objects in chocolate,
consisting sometimes of three or four parts; they are made either
of sheet iron, tinned, or, for more complicated forms, the moulds
are cast in tin, but these latter are not so durable as those of tinned
sheet iron with strong iron frames.
The several parts of the moulds, after having soft chocolate
mass pressed into them, are put together and excess of material
is removed by requisite pressure by the use of a press of the kind
made by A. Reiche in Dresden, which will admit of a large number
of moulds being placed in it at a time. By the use of such a press
the moulds are protected from injury, and the objects moulded have
a better appearance, as a result of the uniform as well as strong
pressure exerted.
After cooling, the moulded objects are readily detached from
the moulds and they only require to be scraped clean, or further
ornamented as may be desired. That is done in various ways, for
example by painting with coloured cacao butter.
4. Crumb Chocolate.
This term is applied to the small pieces of chocolate of
truncated conical shape, with from 4 to 5 smooth surfaces. They are
made by a machine specially constructed for the purpose by A. Reiche
(No. 1550); it consists of a four-cornered box with a removable bottom.
Inside the box there is a false bottom, from 1 to 2 cm above the other
bottom, which is fitted with a removable sheet iron plate, in which
pentagonal holes are stamped. A knife can be introduced at one corner
of the bottom of the box. After sufficient chocolate has been
made to penetrate through the pentagonal holes by agitating the
box on the table, the knife is rapidly drawn across the bottom and
the box raised up. The sheet iron plate is then taken out, and by
gently tapping one corner the small pieces of chocolate are
shaken out.
5. Small tablets, sticks, fruits or figures filled
with cream.
These are prepared by pouring the cream contents in either
wooden or iron moulds, previously dusted with a little flour, and then
moulding round them chocolate in whatever form is required, always
taking care that this is kept as soft and plastic as possible, a suitable
addition of cacao butter proving invaluable for the purpose.
In former times chocolate moulds were manufactured exclusively
in France, where the firm Létang of Paris enjoyed what was
to all intents and purposes a world monopoly. But since the year
1870 the oft-mentioned firm of Reiche in Dresden-Plauen has taken
up the manufacture, and has succeeded in conquering the market in
a remarkably short time. The moulds of this firm satisfy each and
every possible requirement, although it would be no disadvantage
if the old type of pattern mould were cleared away at one and the
same time with the old routine, to make room for a little artistic skill
and embellishment.
Recently Reiche has brought out a special machine intended as
an easy and practical cleanser of his many moulds, which include
bonbon cutters and cutting rollers, numbering stamps, chocolate
slicers, roller machine boxes etc. He has lately brought on to the
market a special machine for quickly and efficiently cleaning the
moulds, which is illustrated in fig. 53.
In one end, a circular brush is introduced, and against this the
moulds to be cleaned are firmly pressed. In consequence of the
large number of revolutions which this brush passes through, the
moulds are cleansed of still adhering masses of chocolate in a half
or third of the time occupied when hand labour is employed. At the
other end of the shaft occurs a duster, sprinkled with Vienna white
(a lime), which polishes off the moulds previously and thoroughly
cleaned by the circular brush. The great advantage of this machine
is that the daily expenditure on polishing is considerably reduced
One girl can do the work of two hand workers, when this machine
is employed. In addition, it makes possible a continual touching up
of the material used in the making of the moulds, a ventilating apparatus
removing all traces of dust.
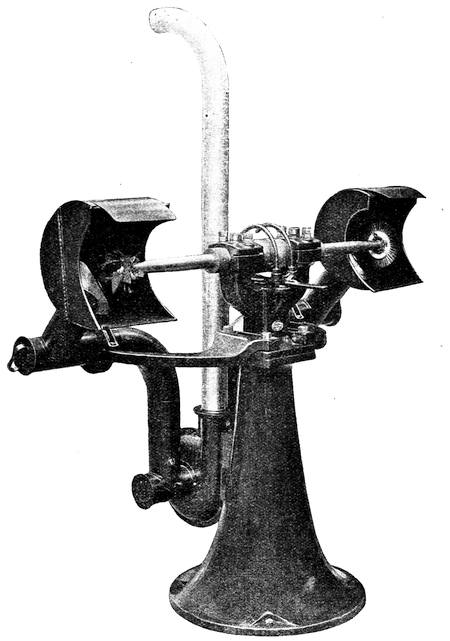
Fig. 53.
12. The Shaking Table.
The pasty chocolate mass fills itself into the chocolate moulds
spontaneously, in consequence of its soft consistency. Yet to share
it evenly throughout the mould, so that it adapts itself to every bend
and hollow there occurring, and further to bring to the surface any
possible bubbles of air evident in the mass, the chocolate is whilst
still in the moulds subjected to brisk shaking.
This is effected by placing the chocolate on trays and transferring
these to the shaking table, of which types and construction
are at the present time manifold and various, the best and oldest being
given in front elevation below (Fig. 54).
Fig. 54.
The movable slab a, fitted with an upright rim at its edges,
has underneath two projecting pieces d, working against deeply toothed
wheels e, which fastened on the shaft b, are driven round by
the pulleys c. The teeth of the wheels catch on the projecting pieces
at every revolution of the shaft and push them rather gently on one
side, and when the tooth-points slide from under the slab, it drops
down as much as it has been previously raised. Each tooth of the
wheel coming into contact with the projections, the same motion
is repeated several times, causing the slab to oscillate up and down.
This oscillation of the slab is controlled by means of a hand
lever f, occurring on the shaft g, and fixed crosswise thereon, so that
we can only show it in cross section on the diagram. The lever f
attaches itself to the under part of the slab, raises it, and so throws
the wheels out of contact with the projecting pieces, but without
stopping the rotation of the shaft b.
Shaking tables have also witnessed considerable improvements
with the lapse of time, and we shall now proceed to treat these in
more detail, especially as several recent constructions offer and
illustrate many interesting mechanical points.
Fig. 55.
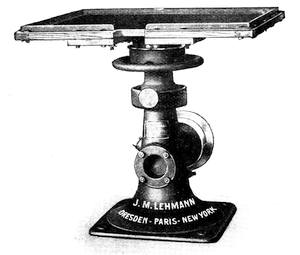
Fig. 56.
An old type of machine, that is nevertheless still much
employed, is illustrated in fig. 55. Here the slab is caused to osculate
by shaking wheels introduced underneath, each possessing six, eight,
or more teeth. The slab is raised and lowered by contact with wedge-shaped
parts, the effect produced being greater or less according as
the moulds are large or small, heavy or light, and in proportion to
the consistency of the chocolate mass which they contain, e. g.
whether it is solid or semi-liquid.
Quite an improved construction is shown in fig. 56. Here the
table is attached to a vertical axle, which is moved up and down by
means of a toothed wheel fixed on its bottom end. There is also a
cylinder arrangement under the whole machine to assist in controlling
the vertical motion of the shaft, and as it is provided with
automatic lubrication, there is no danger of any wearing out of the
apparatus and consequent irregularity of functioning.
The shaking and jerking of the slabs is in itself attended by a
considerable amount of noise, and when to this is added that caused
by the tables, it will be seen that a chocolate factory may become to
its neighbours a very serious source of objection. For years attempts
have therefore been made to construct shaking tables, so that they
would not cause any greater noise than is absolutely inevitable.
Pneumatic contrivances and caoutchouc have met with right royal
success in this connection.
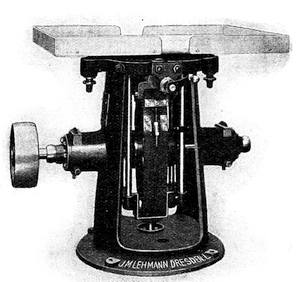
Fig. 57.
The most recent and probably the most perfectly constructed
shaking table is given in figs. 57 and 57 a. It embodies all the latest
improvements and is self lubricating, a fact of the highest importance
as releasing the strain on the attendance, which would need to be
very perfect to ensure absence of noise in the case of a machine
making 800 strokes a minute. When it is considered that the moulding
room is generally managed by girls who neither possess knowledge
of, nor interest in, the machines, the advantages of such automatic
lubrication become even more apparent.
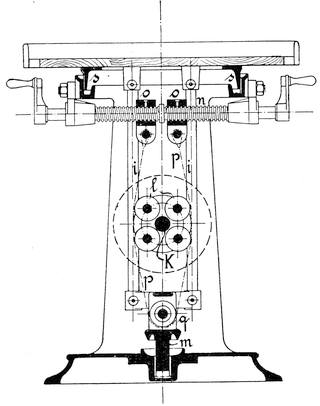
Fig. 57 a.
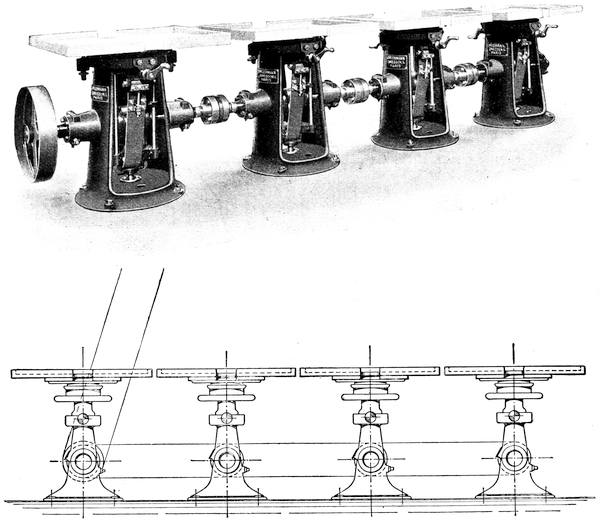
Figs. 58 and 58 a.
Apart from the automatic lubrication, in itself a sufficient
guarantee for the efficiency of the machine, screws and nuts are
entirely avoided on this machine. The motive mechanism is also
interesting. By a special arrangement, the number of revolutions in
relation to the number of the elevations of the slab is reduced to one
fourth, viz., from 760 to 190. Since the elevation of the slab can be
regulated to zero, a loose pulley for shifting the driving belt is
unnecessary; in addition, the driving shaft makes only a small number
of revolutions, and works in oil. The round shaped upright serves
to carry the vertically moving frame i, which supports the slab
moving in an oiled groove at s, and which is supported underneath by
the pivot m. Both at m and s there is automatic lubrication. The
bearings of the spindle n, attached to the upright, work into left and
right screw threads at oo, to which points the ends of a broad leather
belt p are attached, passing over the roller g, by which the
frame i is suspended. The driving pulley k, running in oil, carries in
its centre the four rollers l, which turn round and round the pulley k,
so as to come into contact with the belt p and press it outwards on
both sides. At the same time it shortens the belt in the vertical axle,
so raising up the table slab i. This is repeated four times by one
revolution of the driving pulley, so that working with 190 revolutions
a minute, the slab is raised 760 times. According as the screws oo
are moved to or from the centre, the vertical movement of the slab
can be increased or decreased to a point when the slab is completely
out of action, i. e. when the rollers l no longer touch the belt p. Under
favourable local conditions, a number of such tables can be driven
by one shaft, so that only one pulley and a single driving belt would
be needed, though each table would work quite independently of the
others. Such an arrangement is shown in figures 58 and 58 a.
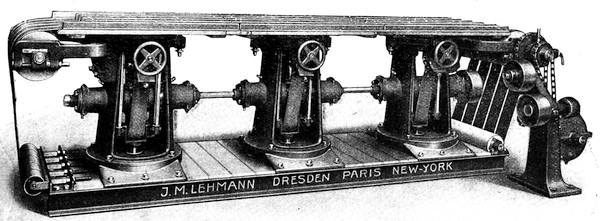
Fig. 58 b.
This shaking table, though only recently introduced, has quickly
made itself popular, and is especially suitable for the preparation of
readily liquefiable chocolate. The gentle vibratory motion produced
by this shaking table and its exact adjustability admit of the
thinnest cakes being made in a perfectly uniform thickness, without
any objectionable projections round their edges. Besides the shaking
tables of this construction there are others made in such a way that
whether the moulds are light or heavy, small or large, the slab is
always raised to the same height, the working of the slab being adjusted
by altering the number of revolutions. The manipulation of
these tables is much more difficult than that of tables constructed as
above described, and that is probably the reason why these have
for decades been scarce on the market.
The moulded chocolate spread out on trays is transferred as
rapidly as possible to the cooling chamber, with which we shall
conclude section IV.
Instead of several shaking tables alternately receiving the
moulds, which involve frequent changes, so-called shaking systems
(fig. 58b) have been generally adopted of late. They consist of a number
of shaking tables, having their frames attached to each other, possessing
a common motor control, and having their slabs arranged one
after the other in such a way that the filled moulds slowly proceeding
from the dividing machine can be automatically conducted over them.
The shaken moulds are then passed on to further processes, or they
enter the cooling chambers at once. The advantage of the shaking
table system lies in a reduction of the number of hands, who only
need to be in attendance at each end of the system, and further in the
regularity, both as regards time and strength, which prevails in
connection with the shaking of each mould.
13. Cooling the chocolate.
Experience has shown that the more rapidly the moulded chocolate
is cooled the finer is its texture and the more uniform the
appearance of the fractured surface. That is due to the formation of
smaller crystals of the fat when the cooling is rapid, while in slow
cooling larger crystals are formed and the fracture consequently becomes
dull and greyish.
Formerly it was possible to distinguish chocolate made in
summer from that made in winter by the more uniform appearance
of the fracture, that was, in the latter case, the result of more rapid
cooling.
At present, however, manufacturers are no longer dependent
upon favorable atmospheric conditions in that respect, for by suitable
arrangements it is now possible to produce the reduced temperature
requisite by artificial means.
The most suitable cooling chamber is an underground space
which should, however, be so situated as to be in convenient communication
with the moulding room. The cheapest and simplest
place for a cooling chamber is a cellar, if it be properly constructed
and dry, as well as large enough to contain the quantity of
chocolate made in one day’s working. The best temperature to be
kept up ranges from 8° to 10° C. Within those limits there is no
danger of the chocolate being coated with moisture, or that it will
acquire a coarse grained texture by lying too long. The following
rules will serve for guidance in regard to this point:
Generally, chocolate presents the finest fracture when it has
been fully levigated and when it contains a considerable amount of
fat, provided that the fat present is only cacao butter. Those kinds
which are not so well levigated, or have had some addition of foreign
fat of higher melting point, show an inferior fracture. It is possible
to obtain an equally vitreous fracture in a less cold cellar (16° C. and
upwards) when the chocolate is moulded at a temperature corresponding
to that of the cellar; to effect that, the chocolate should be
moulded at a proportionally lower temperature the warmer the
cellar is. The difference can be seen by the appearance of pale red
spots on the surface. When it is desired to dispense with artificial
cooling, the cellar should be as much as possible below the surface of
the ground; it should also be of sufficient height, not less than 3 m.
If the situation and height of the cellar be properly adjusted, the
requisite area for disposing of a daily production amounting to 5000
kilos would be 400 sq. m. The cellar must be well ventilated and
furnished with double windows, so placed as to open towards the
north and east. Discharges of warm waste water, as well as steam
pipes or furnaces should be kept as far distant from the cellar as
possible. The internal arrangement of the cellar should be of such
a nature that the whole of the chocolate to be cooled can be deposited
upon the floor, since that is the place where cooling takes place most
rapidly. With that object in view it is desirable to construct brickwork
pillars about 25 cm high, covered with white tiles. Passages
are arranged between these pillars. The cellar should be entered
by as few persons as possible and, therefore, the cooled cakes of
chocolate should be taken at once, in the moulds, to an adjoining
room to be turned out and passed on to the packing room and store.
Most of the existing factories, that have been established for
any time (large and small) have had to adopt artificial means of
cooling, because in most instances the quantity of chocolate to be
cooled daily has, in course of time, increased tenfold. The machine
rooms have been enlarged, the number of machines has also been
increased, while the cooling cellar has remained in its formerly modest
proportions. But those circumstances are not the only reasons for
having recourse to artificial refrigeration, which is often necessary
in consequence of the inconvenient situation of the cellar and the
high underground water level.
In the application of artificial refrigeration in a chocolate factory
it is not advisable to hasten the cooling of large quantities by
producing too low a temperature in small chambers. The cakes of
chocolate mass by that means come out of the moulds as hard as
glass, but it is questionable whether the consumer using the chocolate
many months afterwards, will make the same observation. Great
care would have to be taken with such rapidly cooled chocolate, to
pass it gradually through chambers of a medium temperature and
thus prepare it for exposure in the packing rooms and warehouses.
Even when employing artificial means for cooling, the reduction of
the cellar temperature and cooling upon pillars is to be preferred to
the more direct cooling upon a system of pipes, which after all is
nothing else than a cooling upon ice, as may be in some instances
the only alternative. Consequently, a well constructed cellar for
cooling, furnished with a system of cooling pipes on the roof is perhaps
the most advantageous arrangement, especially for large
factories.
In carrying out artificial refrigeration various kinds of machines
are used for reducing temperature, in which the desired effect
is produced either directly by the condensation and evaporation of
suitable materials, such as liquid carbonic acid, ammonia, sulphurous
acid, or indirectly by making saline solutions (calcium chloride), cooled
below the freezing point, circulate through a system of pipes fitted on
the roof or walls of the space to be cooled. As the cold liquid is
pumped through the pipes, it takes up heat from the air in contact
with them, correspondingly reducing the temperature of the cooling
chamber. The cooling installations of the firm of C. G. Haubold, junior,
Chemnitz, are among the best and have long been extensively used in
the chocolate industry. Their cooling apparatus is a compressing
machine, in which coolness is obtained by the evaporation and recondensation
of such liquid gases as carbonic acid or ammonia. Like
all compressing machines, it is comprised of three main parts.
I. The evaporator or refrigerator, consisting of a wrought iron
system of pipes. The latter are placed in the spaces of the plant
to be cooled, with a so-called direct evaporation arrangement,
and are either arranged on the walls and ceiling, or built in a
special chamber as dry or moist air coolers, according to the
quality of the chocolate to be cooled, or the use for which it is
destined. Whilst in the former case cooling is effected directly
in the rooms, in the latter the air of the cooling room is conducted
to the air coolers by means of ventilator, in order to be
cooled and dried there, and then again introduced in the chamber.
II. The compressor, a gas suction and pressure pump, working both
simply and complex, which draws the refrigerating medium out
of the evaporator, compresses it, and forces it along to the condenser.
III. This condenser consists of a coil of wrought iron or copper pipes,
which are enclosed in a barrel and are often described as the
immersion condenser. There is another type, in which the pipes
are united to one or more pipe-walls, introduced in a vessel which
collects and drains off the condensations. In both cases the coil
of pipes is played upon by a continual stream of water, in order
that the gases which they contain may be condensed. The
immersion condenser is generally employed when there is a
plentiful supply of cheap water at hand, and the other in contrary
cases. This latter condenser is provided with a separate
liquid “after-cooler”, constructed on analogy with the before
mentioned immersion condenser. The counter current principle
holds good in both types, and admits of a better using up of the
cooling water. The liquid gas then passes on to the evaporator,
where it is responsible for further refrigeration.
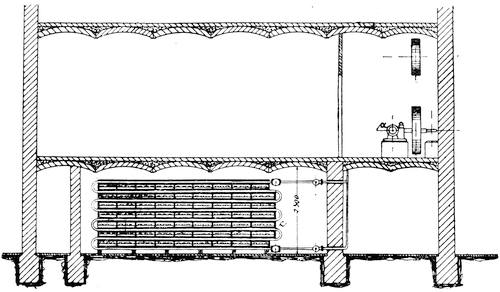
Fig. 59a.
The refrigerator also occurs in the form of a brine cooler. In
this construction the evaporating pipes are likewise enclosed in a
barrel, containing a high percentage of salt brine. In consequence of
the refrigerating apparatus occurring on the interior of the pipes,
the brine contained therein is cooled down to a very low temperature,
pumped along to the cooling chambers, and after delivering its alloted
refrigeration unit re-conducted to the cooling apparatus, where it is
once more subjected to the same series of processes.
A well-known arrangement for such artificial refrigeration is
that constructed by Wegelin & Hübner at Halle o. S., in which carbonic
acid is employed, and it has been found well adapted for use in
chocolate factories. The accompanying illustrations figures 59 a and
59 b represent an arrangement of that kind in which the cooling is
effected on cooling trays judiciously arranged.
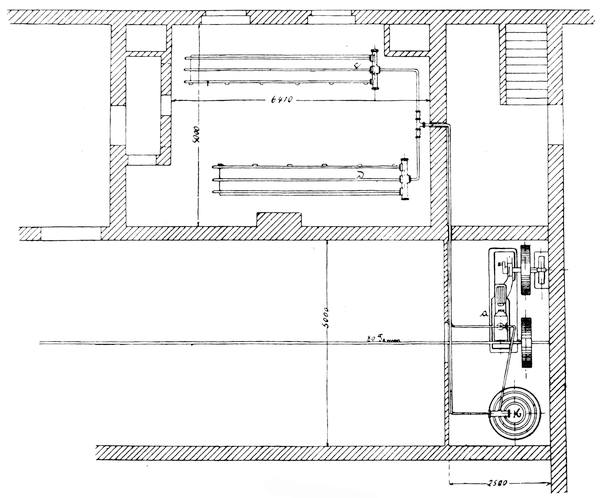
The refrigerating machine is constructed on the carbonic acid
gas compression system; it consists of 1. the compressing pump a,
2. the condenser b, and 3. the system of pipes c and d, that constitute
the refrigerator. The coil of pipes in the refrigerator is connected at
one extremity with the compressing pump and at the other extremity
with the condenser. Liquid carbonic acid passes from the condenser
into the coil of pipes and is there evaporated. The heat necessary
for that change is withdrawn, either directly or indirectly, from the
cooling chamber and from the chocolate placed in it, until the desired
reduction of temperature is brought about.
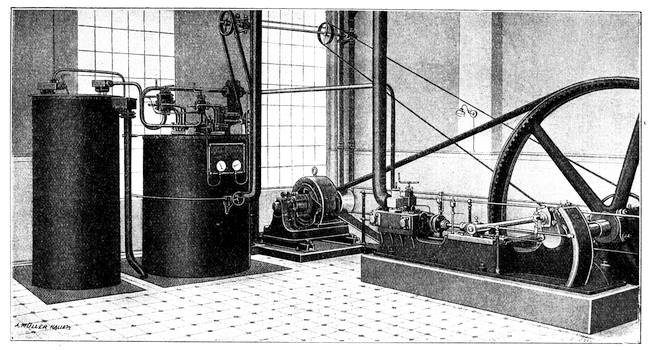
Fig. 60.
The compressing pump a is a peculiarly constructed suction
and pressure pump, it draws out of the refrigerating pipes the
vaporised carbonic acid by which they have been cooled and then
subjects it to a pressure which helps to effect its reconversion into
the liquid state.
The condenser b consists of a coil of pipes over which a
current of cold water is kept flowing and the compressed carbonic
acid vapour, passing from the compressor into these pipes, is there
cooled and condensed by the surrounding water, so as to be transferred
back to the refrigerator through a valve fitted to it for that
purpose. The outer vessel of the condenser is constructed of cast-iron,
in one piece with the compressor frame. These cooling arrangements
are constructed either with or without mechanical ventilators.
In figures 63 a and 63 b the compressing pump and condenser are
represented as placed on the ground floor, while the refrigerator
is situated in the cellar space lying beside them and at a lower level,
in such a manner that both the systems of cooling pipes are not
situated upon the roof of the cellar, but run along it at regular
distances parallel to the side walls of the cellar. The compressor
and condenser form one apparatus and the former is driven by a
steam engine.
In the cooling cellar, the refrigerator is generally fixed to the
walls in such a way that the warm chocolate, taken into the cellar,
can be at once placed upon the stages formed by the system of
cooling pipes, and so there is some advantage in having the system
of cooling pipes fitted along the roof of the cellar.
The machine which is diagrammed in fig. 60 possesses an
hourly output of some 70000 calories, measured in salt water at
-5 ° C. The compressor is driven directly by an electric motor,
and a stirring apparatus is put in motion by the crankshaft of the
compressor, the two being connected by an intermediate gearing.
Wegelin and Hübner put out cooling plants with salt water
cooling, smaller and medium sized plants are on the contrary provided
with so-called direct evaporation.
The diagram in fig. 61 shows an air-cooler as built of late by
Esher, Wyss & Co. for chocolate cooling plants.
These air coolers are especially used for direct evaporation
of carbonic acid gas. They consist of three groups of ribbed wrought-iron
pipes, the whole constituting a system supported in a frame
work of U-shaped and angular iron. The separate tubes are welded
and bent together. The ribbed bodies are in themselves square
shaped, and apart from the tube opening have a nozzle introduced in
their centre, which pressed firmly against the press pipe effects a
favourable transmission of heat in the case of large surface areas
of the support, the more so as the tubes are square shaped.
Among the numerous advantages of this machine can be
numbered the abolition of the refrigerator and brine pump, prompt
and instantaneous refrigeration when the machine is started, and
ease of control, as a flange connection occurs immediately in front
of the machine.
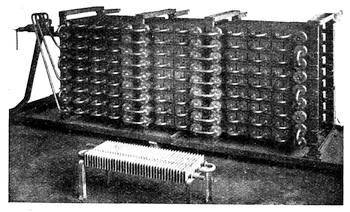
Fig. 61.
A wrought iron trough is fitted up underneath the air-cooler to
catch the water drops. Above, and to the left, the three systems
of the air-cooler are connected by means of a catch.
In the foreground of the illustration is given a miniature of
the ribbed tube system, which very clearly illustrates the arrangement
of the separate ribs.
A ventilator not apparent on the diagram conducts air to
the tubes in the cooling chamber, and these present a considerable
cooling area, in addition to which, the air-stream taking a parallel
direction, resistance to its passage is reduced to a minimum.
Another method of cooling119, that is carried out in France
consists in placing the moulds, containing cakes of chocolate, upon
a travelling belt running horizontally through the whole length of
the cooling chamber. The requisite reduction of temperature is
effected by apparatus similar to that described above in Wegelin &
Hübner’s arrangement. The liquefied carbonic acid flows through a
system of pipes fitted to the roof of the cooling chamber, producing
by its vaporisation the necessary cooling and then it passes back
to the refrigerating machine. Circulation of the air in the cooling
chamber is provided for by a suitable ventilator under the pipes
of the cooling system, gutters being fixed to carry away any water
condensing upon their surface and prevent it from falling upon the
chocolate. The travelling belt passes along so slowly that the
moulds, containing chocolate, placed upon it at one end, take from
ten to fifteen minutes in passing to the other end where they are
taken off and carried to the packing rooms.
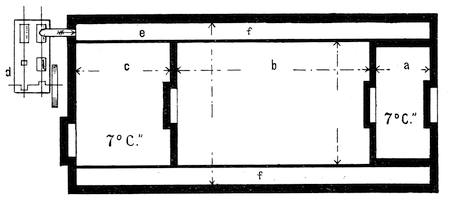
Fig. 62.
Another cooling arrangement that works very well is constructed
by T. & W. Cole of the Park Road Iron Works, London E.;
figure 62, represents a plan of this arrangement, which has the great
advantage of providing for the exclusion of moisture from the
cooling chamber. Refrigeration is effected, by means of Cole’s Arctic-Patent
Dry Cold Air machines, by compressing atmospheric air and
then allowing it to expand, after being cooled by water and having
moisture removed by suitable arrangements. The machine is of
very solid construction; it works at a pressure of from 70 to 80
atmospheres and drives the dry cooled air through a system fitted
in the cooling chamber where the chocolate is spread out, either on
portable trucks or on a travelling belt, so that it remains in the
chamber long enough to become perfectly cold. The system of
cooling can be changed in various ways. The sudden removal of the
cold chocolate into another chamber where the air is moist, would
be attended with a deposition of water upon the goods. For that
reason the goods are first transferred, for a short time, to a warm
chamber (ante-room) where they acquire a temperature at which no
deposition of moisture can take place. The chief advantage of this
arrangement is that it furnishes dry cold air economically, both in
summer and also in a moist climate. Cole guarantees that this machine
will effect a refrigeration of 5 ° C.; according to the statement of
Messrs. Negretti and Zambra the cooled air contains only 40 % of
moisture. The cold air from one of these machines can be led, by a
well insulated run of pipes, to any part of the factory and thus be made
available for cooling purposes in different places.
The cooling plants hitherto described may be classified as “Space
Coolers”, because in each case a special compartment of the cooling
chamber must be utilised. The increased prices of estate constitute
no mean objection to such a system.
A critical valuation of these plants brings out a few undisguisable
deficiencies. A large proportion of the cold is lost in the
chamber itself, before it has been of any avail; and then again the
rooms are generally insufficiently, sometimes even not at all, insulated
from adjacent and warmer chambers, which once more involves
raising of the low temperature essential in the process.120 Detrimental
also is the presence of the personnel, the illuminations, and many
minor influences. It is evident that the larger the output required
the larger must the cooling chamber be, involving corresponding
economical waste.
With the recognition of these evils arose the problem of their
abolition. The aim was to employ small chambers and avoid loss of
cold air. It is now solved by a system already used in many and
various industries, namely, cooling in closets. Larger or smaller
closets may be employed, as required, and in consequence of their
thorough insulation may even be introduced into the warmest rooms.
Their principle is maximum efficiency with minimum occupation of
space, and avoidance of loss of cold as far as possible. In consequence
of this latter aim, the refrigerators in this case can be
constructed on a smaller scale than those destined for an equal output
of material, which are fixed up in cooling chambers; or they may
be larger, which is yet more important, for the efficiency of the
machine under consideration can be considerably increased by
connecting it with one of the closets.
There are two sorts of cooling chambers, those which transport
the moulds automatically, and those which contain layers where the
moulds are placed one over another. Both types are cooled by the
circulation of air, so effected, that cooled air currents are sucked up
by a fan out of a tubular system fitted underneath a horizontal partition,
and then forced along to the chambers above, where they are
evenly distributed over the rows of sheet-iron, laden with moulds, or
where they play upon the travelling belt which transports the moulds
out of the cooling chambers. The air passes once more into the tube
chamber on the opposite side, where it delivers up the warmth it has
in the meantime acquired, to enter finally the same system of circulation
as before. The general temperature of the closets is a mean
between 8 ° C. and 10 ° C., and the cooling lasts from 20-40 minutes,
according to the strength and size of the tablets. As the temperature
never goes lower than 8 ° C., it is impossible for the tablets to become
moist when exposed to the warmer outer atmosphere. Fig. 63a
shows a Cooling Chamber built by J. M. Lehmann, which is adapted
for a daily output of some 1000 kilos, and divided into compartments
one above the other. The sections of this chamber, which in the
illustration plainly shows the small amount of space required for its
erection, are divided by vertical cross-partitions into four compartments,
each of which is provided with a shelf or stand to take a
charge of 10 cooling trays, and accessible by three spring-doors, thus
giving as small apertures as possible and reducing the loss of cold
when charging to a minimum. In addition to this, each compartment
is fitted with a contrivance for regulating and, if necessary, completely
cutting of the draught. The position of the system of pipes is shown
by the two pipe-ends to which it is connected. On the opposite side,
or front of the chamber, is the fan-drive, either a small electric motor,
or shafting. The perforated cooling trays are visible through the
open doors. The sides of the chamber consist of two layers of wood
with thick slabs of cork between them. All chambers of this system,
including those with automatic conveyance of the moulds, can be
taken to pieces for transport, the single pieces afterwards only requiring
to be fastened together again when erecting the chamber.—The
chamber illustrated serves for cooling moulded chocolate. For
pralinés and the like similar chambers are supplied, which are,
however, smaller and lighter in construction.
Fig. 63b represents a cooling chamber with forced air circulation
and automatic conveyance of the moulds, built by the same
firm. This chamber, which, owing to the travelling belt conveying
the moulds, is of considerable length, is nowhere connected with the
outside air; the whole manipulation of the moulds is carried on
through small adjustable openings at the points where the travelling
band enters and leaves the chamber. The band consists of chains
in links on to which wooden laths are screwed and its speed can be
regulated to suit the size of the tables to be dealt with. The width
of the belt and chamber can at any time be varied to suit the place of
erection and correspond with the length.
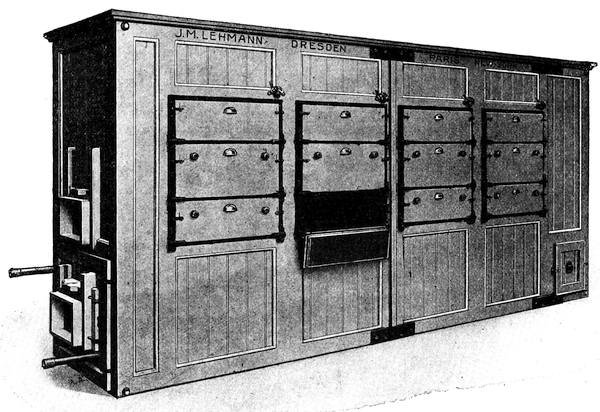
Fig. 63 a.
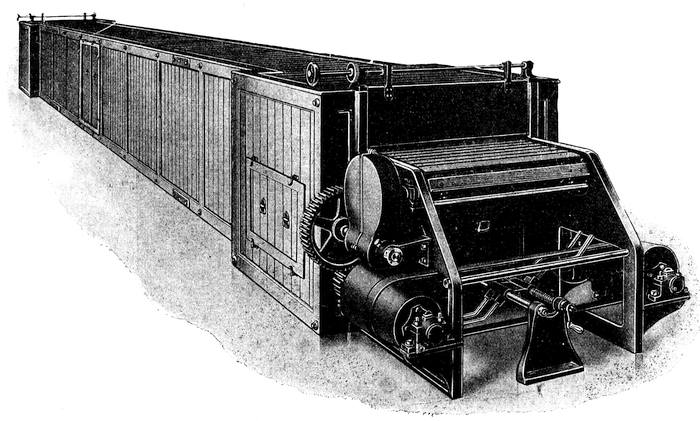
Fig. 63 b.
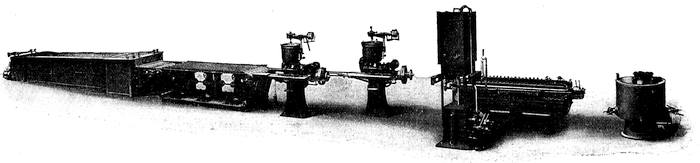
Fig. 63 c.
As is to be seen from the illustration, this cooling chamber requires
the minimum of attendance and thus complies with the principles
lately adopted in all large factories, in which the tendency is
to substitute as much as possible mechanical appliances for manual
work. It will be seen from the preceding chapters that this tendency
is especially marked in the moulding department, where automatic
tempering, moulding and mould-filling plants and shaking tables have
already been introduced. In order to utilise fully such automatic
plants the last link in the chain only was wanting, namely, a suitable
means of transferring the moulds from the shaking tables to the cooling
chamber and through the latter to the demoulding and packing
room. The purpose of the cooling chamber above described is to
fill up this gap, and its proper place is thus ranged in among the automatic
machinery described.
Thus it is that many modern factories have united the above
machines to form a single working plant, as shown by Groundplan
Fig. 63c.
a) Chocolate Lozenges and Pastilles.
These chiefly consist of cacao mass, sugar and spices. Formerly
they were made by placing the semi-liquid chocolate material
on a stone slab, furnished with a rim of uniform height which served
to regulate the thickness of the goods manufactured, and then
rolling out the mass as required. The lozenges were punched from
the rolled-out layer by means of a cutter. After allowing the mass to
cool, these lozenges were detached from the remaining portions, which
were then rolled again and the same process repeated.
Pastilles, on the surface of which impressions of varying import,
such as figures, names, firms etc. are required, may also be manufactured
by placing the soft chocolate mass upon tin-plates in which
depressions occur corresponding to the device desired. A roller is
employed to make the material fit into the depressions, and superfluous
chocolate is removed with a knife.
These impressions come out especially fine, when the pastille
moulds are subjected to a shaking on the tables with which we are
already acquainted.
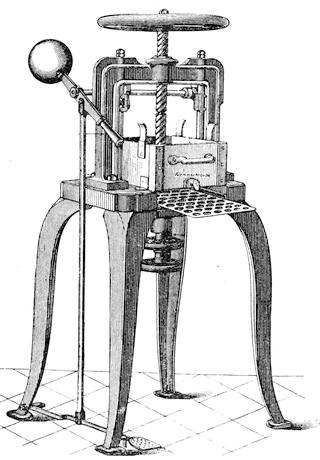
Fig. 64.
Fig. 65.
Yet these processes are becoming obsolete, and the chocolate
slabs or plates are at the present time superseded by the two forms
of apparatus constructed by A. Reiche, which we accordingly describe
below.
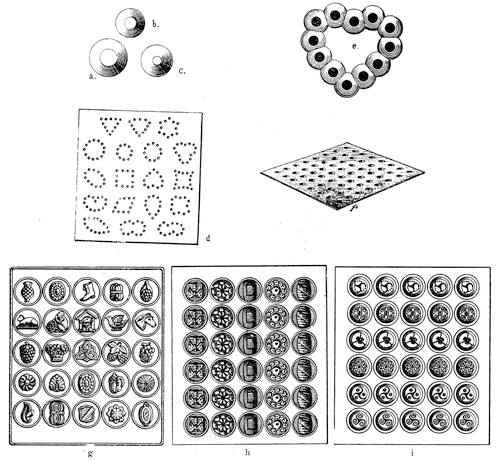
Fig. 66.
In the first of these simply constructed machines, fig. 64, the
material oozes through perforations in a square sieve-like arrangement,
at length issuing on the sheet-iron plate fitted underneath. The
process is aided by repeated shaking, and when sufficient chocolate
has penetrated to the plate, the box is raised on its hinge and chocolate
mass left ready for further treatment. By gentle additional
shaking, the still irregular heaps are rounded off to perfection; they
are now cooled down and finally detached. The coating of the
lozenges with coloured sugar grains is effected by passing them,
together with the plate to which they still adhere, through a box
containing sugar dust.
This machine is scarcely used now; in its place come the two
constructions of A. Reiche, as already stated, the one being intended
for solid material, and the other for semi-liquid chocolate mass.
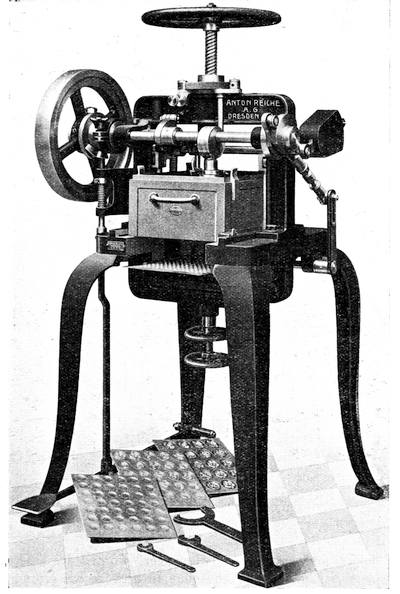
Fig. 67.
By means of his pastille machine Nr. 14091, which we give in
Figs. 65 and 66, chocolate lozenges of the most diverse size can
be prepared very rapidly and to advantage. The chocolate material,
which in this case is solid, is pressed through perforations in a metal
plate and otherwise treated as in previous cases.
In working with this machine, it must be previously and sufficiently
warmed, then partially filled with chocolate material of a
proper consistency (not more than 75 % of the total capacity may be
utilised). It is highly important in the preparation of lozenges that the
material should neither be too hard nor too plastic, but strike a just
medium.
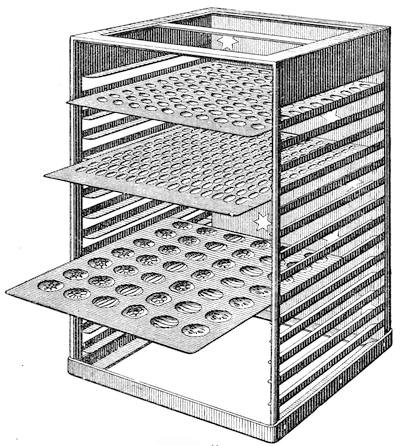
Fig. 68.
Before pressing down the plunger, worked by a screw, a
metal plate is laid upon the chocolate to prevent contact with the
plunger. By slight pressure, the chocolate mass is forced through the
perforations, according to the required size of the lozenges, but the
plunger must not be screwed down further. This will admit of the
plate on which the lozenges rest being drawn out and another
inserted.
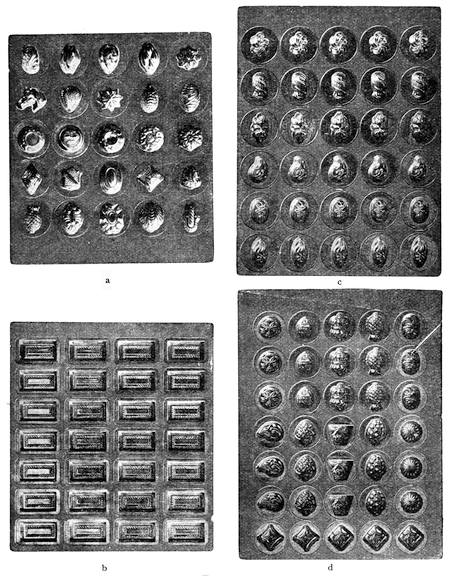
Fig. 69.
To this machine belong the usual perforated plates f, Fig. 66 of
which there are three of different sizes for each machine, as shown by
figures a b c, also the plates d used for making the perforated confections
which find their way to the Christmas Tree. These plates
are impressed with larger or smaller designs, and so make two different
sizes of goods possible. A third plate is supplied for the
manufacture of whole pieces (various varieties of chocolate croquette).
The machine works smoothly and noiselessly and delivers
excellent products. If instead of the usual plain lozenges, such with
the name of a firm or other device are desired, the corresponding
impressions must be stamped out on the plate in which the chocolate
is received after being forced through the perforations. See fig. 66,
g, h, i.
Fig. 67 illustrates the pastille machine Nr. 14 178 for thin chocolate
mass, constructed by A. Reiche (German Patent 227 200). It
resembles the foregoing apparatus in principle and appearance, being
only distinguished by a different aim, namely the treatment of thin
material. Used in conjunction with the peculiar moulds also manufactured
by the same firm (marked “Durabula”), even the deepest
impressions can be effected with an enormous saving of time and
material and in a most practical manner, as will be seen on comparing
figs. 69 a to d.
In order to get the full value out of this machine, some little
practice is necessary on the part of the workman in charge. But
possessed of an average amount of skill, he can soon turn out with this
apparatus ten times as much as can be made with the ordinary type
of lozenge machine.
For a favourable accommodation of the different pastille plates,
the hurdle diagrammed in fig. 68 (by A. Reiche) is quite excellent. It
is manufactured out of one complete sheet of steel, is free from any
suspicion of soldering, and entirely galvanised. It thus offers a
strong guarantee as regards wear and tear. It may also be advantageously
employed as a transporting device.
b) Coated chocolates, pralinés etc.
These delicacies are now held in high esteem, and of late the
consumption of pralinés and cheaper forms with imitative contents
has increased very considerably.
The designation praliné (properly pronounced prahlin) has
been applied to sugar-coated almonds and is derived from the name
of a cook in the employ of Marshal du Plessis, which was Pralins.
This “chef” belonged to the age of Louis XIV. and was the first to
make these sweetmeats. But now the term is applied to sweetmeats
of various forms, soft fruit-sugar, marmalade, cream, nut-paste etc.
respectively enveloped in chocolate. The special formulae employed
in the preparation of different kinds of pralinés are comprised in the
confectioner’s art, and do not need to be dealt with here.
The substances themselves are called fondants. Formerly the
sugar was boiled, placed upon a slab, and there manipulated with a
spatula, an operation difficult to manage, indeed almost impossible in
the last stages. In consequence of the increased demand for such
preparations, machines were introduced several years ago whereby
the operation is mechanically performed. Such a machine is shown
in fig. 70.
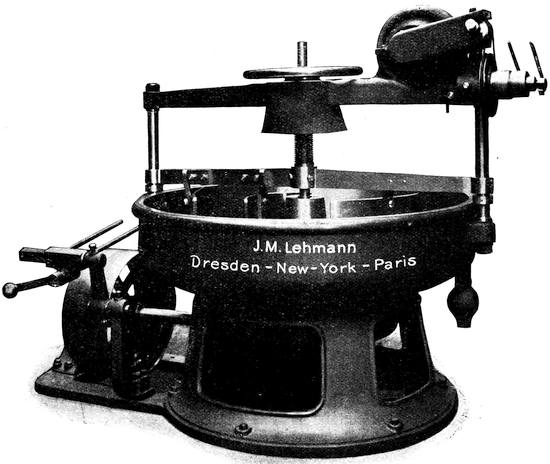
Fig. 70.
The bed-plate as well as all the working parts of the machine
are constructed of stout copper. The working parts admit of being
raised or lowered by means of the hand-wheel above, and they
remain fixed whilst the bed-plate turns and its underside is played
upon by water. The machine is capable of working up pure fondant
without any syrup addition, as well as that made up with syrup. The
boiled sugar is poured on the bed-plate of the fondant machine, cooled
down from 10-20 minutes according to the syrup content, and to
such an extent that the machine can be set in motion, whilst the
working parts are gradually lowered to the previously mentioned
bed-plate. The sugar poured out is then cooled by means of the
action of a ventilator fitted on a crossbeam, occurring in the middle
of the wooden cooler, and working in conjunction with the ventilator,
in consequence whereof a cooling current of air is brought to strike
the hot sugar centrally.—When pure sugar is used, the fondant is
finished within six minutes, but in the case of a syrup addition the
time required is lengthened.
Fig. 71.
A quite recent type of fondant machine is given in fig. 71.
It achieves its end by employing an air-current and a cylinder
with screw, which is provided with water cooling apparatus.
The modus operandi presents many and obvious advantages,
chief among which is the possibility of conducting new material
to the machine uninterruptedly, and further the preservation of the
flavour of the chocolate worked up. The result is a production of
first-class quality in respect to taste and flavour, which is quite ready
to be passed on to the next processes.
Fig. 72.
The fondant is then diluted with colouring matter in boiling
pans, and so prepared for subsequent treatment. The figures which
have to be poured in are then transferred to gypsum moulds, lined
with starch powder, and the fondant sugar is in its turn poured over
these either by means of pans held in the hand or such as are machine-driven.
Hand-pouring postulates a considerable amount of skill on the
part of the man in charge, especially when even weights of the separate
pieces are required. We annex an illustration of a motor-driven
depositing machine (fig. 72).
The sugar is here introduced into receivers heated by means
of a water-bath. The receiving boxes are moved under the
outflow one after another, after having been dusted with powder and
filled with chocolate, whilst the adjustment of the weight of each
separate piece is effected by the operation of a very ingenious
mechanism, even from 0-8 grammes.
Fig. 73.
After a stay of several hours in the drying room, the molten
figures are so hard that they can be raised out of the powder with
the aid of a shovel. Fig. 73 shows such a machine, whilst Fig. 74
illustrates a machine where the work goes on unbrokenly, and from
which the chocolate figures are removed with a shovel.
The sweetmeats are next dipped into liquified chocolate (covering
stuff) to coat them with a layer of that material. The mass
employed for this purpose must contain up to 15 % more butter than
that used for ordinary chocolate, so that it may be kept soft long
enough for continuous working.121 This is performed in the machine
fig. 75. On a bed-plate coming into contact with steam or cold
water, as required, occur rake-like stirrers, and a small ventilator
introduced above assists in cooling off the material. For the purpose
of discharging, there is an outlet on the rim of the pan. For
storage of the tempered coverings and also for occasional alleviations
with cacao butter, a machine illustrated in fig. 76 is utilised.
Fig. 74.
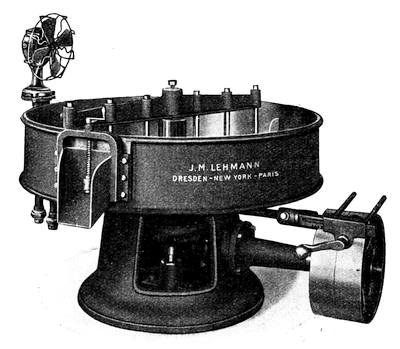
Fig. 75.
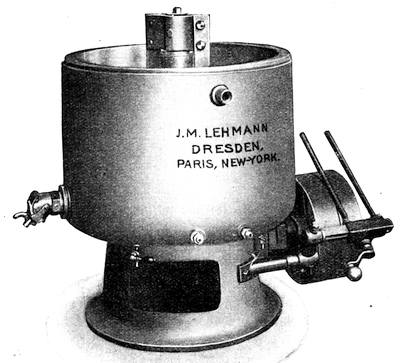
Fig. 76.
The dipping of pralinés for the purpose of coating them was
formerly carried out by means of a fork, the nucleus masses being
dropped into the coating material, taken out with a fork, and placed
upon metal plates. Various kinds of ornamentation were designed
by the same instrument. In the preparation of the higher priced
coated fondants, a similar method of procedure is still in vogue,
although such manipulation presupposes a high degree of skill on the
part of the mechanics are at the machine. For articles of more
general consumption, whether ornamented or not, machines have been
introduced for the purpose by divers manufacturers, some of which
function excellently. Two of that kind which in every way respond
to the calls made on them are here described, but we shall not waste
time and labour over the more complicated and expensive machines.
Fig. 77.
Fig. 78.
The first method of coating fondants, patented by A. Reiche of Dresden-Plauen,
is not based on mechanical principles, but rather relies on a series of
small appliances, represented in fig. 77. The jacketed casing a, fig. 77 contains
water, and into it the pan containing coating material can be placed: that is
kept in a liquid condition by heating the water in the jacket by spirit lamps or
gas jets underneath. The adjoining vessel b is closed on all sides, filled with
water, and also kept warm in the same manner; it serves for the preparatory
warming of the objects to be coated, which are spread upon a wire network,
and for that purpose two of these wire frames can be hung upon the hooks
inside the box. The mass dropping from the wire frame is conveyed into the
covering box a, by means of a sheet of metal placed above it; c serves as an
apparatus for turning, and we give it on a larger scale in fig. 78.
Fig. 79.
The tracings h and i in fig. 79 show the cross section and top
view of the wire gratings, on which cylindrical and ball-shaped sugar
goods are deposited. The other two kinds of grating are illustrated
at L and M (fig. 80).
The size of the meshes of the sieve gratings depends on that of
the centres to be coated.
The method of covering is as follows:
The centres for the pralinés etc. are placed in the cavities of the
gratings, and, as soon as one of the gratings is full, the latter is covered
up by the fine-meshed grating the half of the cross-section of
which is shown in Fig. 79 and the full view in Fig. 80 (see K and N
respectively), K representing the cover-grating.
Both gratings are held simultaneously by the operator at their
handles and then dipped together in the liquid covering contained in
the vessel a, Fig. 77, after which the superfluous covering mass is
removed by knocking. The gratings are now deposited on the
mechanism C, Figs. 77 or 78, as the case may be, the top sieve removed
and a sheet of paper or a metal plate put in its place. It is
then turned by hand to the opposite side, the grating with the impressions
is removed and the cover centres are found lying in regular
order, and at regular distances apart, on the metal plate. The object
of the intervals between the covered centres is to prevent the running
together of the latter.
Fig. 80.
Beans and rings are only dipped up to the middle, and the
process repeated with the other half of the centre after the first half
has cooled. This ensures a pleasing, round appearance, and has
further the advantage that the cover grating need not be put on
during the operation. When dipping cylindrical or ball-shaped
centres, the grating K which has first been removed on dipping, is at
once transferred to the heater, to prevent it cooling and withdrawing
too much warmth from the covering material at the next immersion.
The dipping of pralinés etc. is exceedingly easy if the new
type of dipping machine is used, a full view of which is given in
Fig. 81 and which has the highly appreciable advantage of simultaneously
cooling the dipped centres. All the parts are, in the main,
worked by hand, only the shaking and stirring contrivances and the
cooling fan requiring to be driven by motor power. The middle
piece carries the actual dipping apparatus, underneath which the
tank holding the covering chocolate is fixed, while the lefthand sidepiece
serves for feeding; as many as four operators can be engaged
simultaneously at the latter, the work consisting of laying the centres
in the gratings corresponding to the mouldings desired. The construction
of these gratings is, in the main, similar to the stamped
trays of Anton Reiche, but they are not provided with handles and
are despatched along the guide-rails by hand. The filled grating is
then placed in a frame, which is dipped by means of a winch into
the liquid chocolate. The top grating on the dipping frame is adjustable,
and the object of this grating is to keep the centres down,
as without this arrangement some of the centres might rise to the
surface of the covering. The top grating is, before commencing to
dip, pushed over the filled grating with the centres and is thus immersed
with them. The frame having been removed, the shaker is put
in action to remove the superfluous material from both the gratings
and the centres. The grating is drawn out after use from below the
top grating and transferred to a book-shaped ejector, on one side
of which is a metal sheet covered with paper. The whole of the
centres are then discharged on to the sheet, by reversing the two
flap-sections.
The sheet containing the covered centres is then transferred
to the cooling apparatus at the right, in which it is gradually lowered
on a “paternoster” apparatus by turning round a handle. It is then
conducted to the left by an endless band, and finally discharged in a
cooled state by the machine. The ventilator should be supplied with
air from the cellars and is arranged to blow it out in the opposite
direction to the goods in the cooling apparatus.
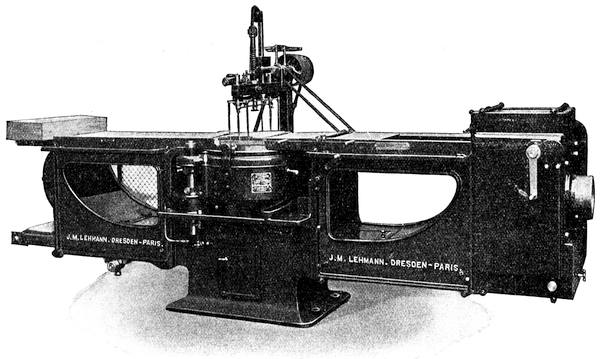
Fig. 81.
The shape of the design-gratings is reproduced in high relief
on the goods, and it will therefore be readily understood that further
designs or fancy shapes can be made on the gratings. For the production
of semi-dipped goods or such as are dipped round and remain
uncovered at the bottom, a device is attached to the striking gear
which renders it possible to regulate the depth of each immersion at
will. The tank containing the covering material is surrounded by a
water-jacket, which is heated by steam. The heat of the water is
indicated by a thermometer. The receptacle containing the covering
can easily be drawn out towards the front. In addition to this, the
whole of the outside of the machine, which also constitutes a complete
water-jacket, is heated by steam, and finally the ejector. The
gratings containing the impressions are taken out of the ejector after
use and transferred to the feeding side to be used again, so that, at
the very most, four gratings are required for each design.
The daily output of the machine is 300-600 kilos, and the size
of the gratings 280 by 400 millimetres, the output naturally depending
on whether the machine is operated by two, three or more persons.