Discoveries and Inventions of the Nineteenth Century
Whole book · 43 sections
DISCOVERIES AND INVENTIONS OF THE NINETEENTH CENTURY
Transcriber's Note:
The cover image was created by the transcriber and is placed in the public domain.
PLATE I.
THE GREAT WHEEL IN ACTION.
DISCOVERIES AND INVENTIONS
OF THE
NINETEENTH CENTURY
Who saw what ferns and palms were pressed
Under the tumbling mountain’s breast,
In the safe herbal of the coal?
But when the quarried means were piled,
All is waste and worthless, till
Arrives the wise selecting Will,
And, out of slime and chaos, Wit
Draws the threads of fair and fit.
Then temples rose, and towns, and marts,
The shop of toil, the hall of arts;
Then flew the sail across the seas
To feed the North from tropic trees;
The storm-wind wove, the torrent span,
Where they were bid the rivers ran;
New slaves fulfilled the poet’s dream,
Galvanic wire, strong-shouldered steam.
Emerson.
BY
ROBERT ROUTLEDGE, B.Sc.,
SOMETIME ASSISTANT EXAMINER IN CHEMISTRY AND IN NATURAL PHILOSOPHY TO THE UNIVERSITY OF LONDON
THIRTEENTH EDITION
Revised and Partly Re-written, with Additions
CONTAINING FOUR HUNDRED AND FIFTY-SIX ILLUSTRATIONS
LONDON
GEORGE ROUTLEDGE AND SONS, Limited
BROADWAY, LUDGATE HILL
1900
PREFACE.
v
In the following pages an attempt has been made to present a
popular account of remarkable discoveries and inventions which
distinguish the XIXth century. They distinguish it not merely in comparison
with any previous century, but in comparison with all the centuries
that have preceded, in regard to far-reaching intellectual acquisitions,
and to material achievements, which together have profoundly affected
our ways of thinking and our habits of life. In the latter, the enormously
increased facilities of locomotion and international communication due to
railways and steam navigation have wrought the greatest changes. These
inventions depending primarily upon that of the steam engine, this
first claims our notice, although properly assignable to a period preceding
our era by a few years. Again, much of our material advancement
is connected with improvements in the manufacture of iron and
its applications in the form of steel, which have been especially the work
of the last half of the century. So great has been the progress in this
department, that for the present edition it has been found necessary to
re-write altogether the article devoted to it. Our social conditions have
also been greatly modified by the celerity of verbal intercourse afforded
by the telegraph and the telephone, and these inventions have received
appropriate notice in this work. In every branch of science also we have
reason to be proud of the discoveries our era can claim, for they vastly
excel in number and are not inferior in range to those of all the ages
taken together. From so large a field, selection was of course necessary;
and the instances selected have been those which appeared to some
extent typical, or those which seemed to have the most direct bearing
on the general advance of our time. The topics comprise chiefly
those great applications of mechanical engineering and arts, and of
physical and chemical science, in which every intelligent person feels
concerned; while some articles are devoted to certain purely scientific
discoveries that have excited general interest.
The author has aimed at giving a concise but clear description of the
several subjects; and that without assuming on the part of the reader
any knowledge not usually possessed by young persons of either sex who
have received an ordinary education. The design has been to treat the
visubjects as familiarly as might be consistent with a desire to impart real
information; while the popular character of the book has not been considered
a reason for regarding accuracy as unnecessary. On the contrary,
pains have been taken to consult the best authorities; and it is only
because the sources of information to which the author is under obligation
are so many, that he cannot acknowledge them in detail.
The present edition has been revised throughout, and such changes
have been made as were required to bring the matter into accordance
with the progress that has taken place since this book was first published
in 1876. But details given in the former editions have at the same time
been retained where they served to indicate the successive stages of
improvement. It would, for example, be impossible in a section on steam
navigation, to omit some notice of the Great Eastern, and therefore the
drawings and the account of the construction of that remarkable ship that
appeared in the first edition, have been left with but slight alterations in
the present volume, although the vessel has since been broken up. On
the other hand, two sections are devoted to projects which the XIXth
century has not seen realised; but the XXth century will in all probability
shortly witness the completion of one or other of the great canal
schemes; and if the first submarine tunnel is destined not to be one
connecting England with the Continent, it will be one uniting Great
Britain with her sister isle.
1899.
viiFor permission to make use of illustrations in this volume the author’s
and publishers’ thanks are due to the several proprietors of The Graphic
(for Plates I., XI., and XII.)—of The Engineer (for sketch design of the
Great Wheel, map and views of the Tower Bridge)—of The Scientific
American (map of North Sea Canal); also to Mr. Walter B. Basset
(for Plate V.)—to “The Cassier Magazine Company” (for Edison’s
Kinetographic Theatre and the Hotchkiss Gun)—to “The Century
Company” (for portrait of M. Tesla, from a photograph by Sarony)—to
“The Incandescent Gas Light Company” (for cuts of burners,
etc.)—to The Engineering Magazine, and The Engineering News, both
of New York—to the Remington Company—to Mr. W. W. Greener, of
Birmingham (for cuts of rifles, etc., from his comprehensive book on
“The Gun”)—to The Photogram, Limited—to the Proprietors of Nature—to
the Linotype Company—and to Captains Hadcock and Lloyd (for
illustrations of modern artillery from their great work on the subject).
Only by knowledge of Nature’s laws can man subjugate her powers
and appropriate her materials for his own purposes. The whole
history of arts and inventions is a continued comment on this
text; and since the knowledge can be obtained only by observation
of Nature, it follows that Science, which is the exact and orderly
summing-up of the results of such observation, must powerfully contribute
to the well-being and progress of mankind.
Some of the services which have been rendered by science in promoting
human welfare are thus enumerated by an eloquent writer: “It has lengthened
life; it has mitigated pain; it has extinguished diseases; it has increased
the fertility of the soil; it has given new securities to the mariner;
it has furnished new arms to the warrior; it has spanned great rivers and
estuaries with bridges of form unknown to our fathers; it has guided the
thunderbolt innocuously from heaven to earth; it has lighted up the night
with the splendour of the day; it has extended the range of the human
vision; it has multiplied the power of the human muscles; it has accelerated
motion; it has annihilated distance; it has facilitated intercourse,
correspondence, all friendly offices, all dispatch of business; it has enabled
man to descend to the depths of the sea, to soar into the air, to penetrate
securely into the noxious recesses of the earth, to traverse the land in cars
which whirl along without horses, to cross the ocean in ships which run ten
knots an hour against the wind. These are but a part of its fruits, and of
its first-fruits; for it is a philosophy which never rests, which has never
attained, which is never perfect. Its law is progress. A point which yesterday
was invisible is its goal to-day, and will be its starting-point tomorrow.”—(Macaulay).
2Thus every new invention, every triumph of engineering skill, is the
embodiment of some scientific idea; and experience has proved that discoveries
in science, however remote from the interests of every-day life
they may at first appear, ultimately confer unforeseen and incalculable
benefits on mankind. There is also a reciprocal action between science
and its application to the useful purposes of life; for while no advance is
ever made in any branch of science which does not sooner or later give rise
to a corresponding improvement in practical art, so on the other hand every
advance made in practical art furnishes the best illustration of scientific
principles.
The enormous material advantages which this age possesses, the cheapness
of production that has placed comforts, elegancies, and refinements
unknown to our fathers within the reach of the humblest, are traceable in
a high degree to the arrangement called the “division of labour,” by which
it is found more advantageous for each man to devote himself to one kind
of work only; to the steam engine and its numerous applications; to increased
knowledge of the properties of metals, and of the methods of
extracting them from their ores; to the use of powerful and accurate tools;
and to the modern plan of manufacturing articles by processes of copying,
instead of fashioning everything anew by manual labour. Little more
than a century ago everything was slowly and imperfectly made by the
tedious toil of the workman’s hand; but now marvellously perfect results
of ingenious manufacture are in every-day use, scattered far and wide, so
that their very commonness almost prevents us from viewing them with
the attention and admiration they deserve. Machinery, actuated by the
forces of nature, now performs with ease and certainty work that was
formerly the drudgery of thousands. Every natural agent has been pressed
into man’s service: the winds, the waters, fire, gravity, electricity, light
itself.
But so much have these things become in the present day matters of
course, that it is difficult for one who has not witnessed the revolution produced
by such applications of science to realize their full importance. Let
the young reader who wishes to understand why the present epoch is worthy
of admiration as a stage in the progress of mankind, address himself to
some intelligent person old enough to remember the century in its teens;
let him inquire what wonderful changes in the aspect of things have been
comprised within the experience of a single lifetime, and let him ask what
has brought about these changes. He will be told of the railway, and the
steam-ship, and the telegraph, and the great guns, and the mighty ships
of war—
“The armaments which thunderstrike the walls
Of rock-built cities, bidding nations quake,
And monarchs tremble in their capitals.”
He will be told of a machine more potent in shaping the destinies of our
race than warlike engines—the steam printing-press. He may hear of a
chemistry which effects endless and marvellous transformations; which
from dirt and dross extracts fragrant essences and dyes of resplendent
hue. He may hear something of a wonderful instrument which can make
a faint beam of light, reaching us after a journey of a thousand years, unfold
its tale and reveal the secrets of the stars. Of these and of other inventions
and discoveries which distinguish the present age it is the purpose of
this work to give some account.
3
STEAM ENGINES. — THE LOCOMOTIVE. — PORTABLE ENGINES. — THE STEAM HAMMER.
To track the steps which led up to the invention of the Steam Engine,
and fully describe the improvements by which the genius of the illustrious
Watt perfected it at least in principle, are not subjects falling within
the province of this work, which deals only with the discoveries and inventions
of the present century. But as it does enter into our province to
describe some of the more recent developments of Watt’s invention, it
may be desirable to give the reader an idea of his engine, of which all the
more recent applications of steam are modifications, with improvements
of detail rather than of principle.
Watt took up the engine in the condition in which it was left by Newcomen;
and what that was may be seen in Fig. 2, which represents Newcomen’s
atmospheric engine—the first practically useful engine in which a piston
moving in a cylinder was employed. In the cut, the lower part of the
cylinder, c, is removed, or supposed to be broken off, in order that the
piston, h, and the openings of the pipes, d, e, f, connected with the cylinder,
may be exhibited. The steam was admitted beneath the piston by the
attendant turning the cock k, and as the elastic force of the steam was
only equal to the pressure of the atmosphere, it was not employed to raise
the piston, but merely filled the cylinder, the ascent of the piston being
caused by the weight attached to the other side of the beam, which at the
same time sent down the pump-rod, m; and when this was at its lowest
position, the piston was nearly at the top of the cylinder, which was open.
The attendant then cut off the communication with the boiler by closing
the cock, k, at the same time opening another cock which allowed a jet
4of cold water from the cistern, g, to flow through the opening, d, into the
cylinder. The steam which filled the cylinder was, by contact with the
cold fluid, instantly condensed into water; and as the liquefied steam
would take up little more than a two-thousandth part of the space it
occupied in the gaseous state, it followed that a vacuum was produced
within the cylinder; and the weight of the atmosphere acting on the top
of the piston, having no longer the elastic force of the steam to counteract
it, forced the piston down, and thus raised the pump-bucket attached to
the rod, m. The water which entered the cylinder from the cistern, together
with that produced by the condensation of the steam, flowed out of
the cylinder by the opening, f, the pipe from which was conducted downwards,
and terminated under water, the surface of which was at least 34 ft.
below the level of the cylinder; for the atmospheric pressure would cause
the cylinder to be filled with water had the height been less. The improvements
which Watt, reasoning from scientific principles, was enabled to
effect on the rude engine of Newcomen, are well expressed by himself
in the specification of his patent of 1769. It will be observed that the
machine was formerly called the “fire engine.”
Fig. 2.—Newcomen’s Steam Engine.
Fig. 3.—Watt’s Double-action Steam Engine.
“My method of lessening the consumption of steam, and consequently
fuel, in fire engines, consists of the following principles:—First. That
vessel in which the powers of steam are to be employed to work the
engine (which is called the cylinder in common fire engines, and which I
5call the steam-vessel), must, during the whole time the engine is at work,
be kept as hot as the steam that enters it; first, by enclosing it in a case
of wood, or any other materials that transmit heat slowly; secondly, by
surrounding it with steam or other heated bodies; and thirdly, by suffering
neither water nor any other substance colder than the steam to enter or
touch it during that time.—Secondly. In engines that are to be worked
either wholly or partially by condensation of steam, the steam is to be
condensed in vessels distinct from the steam-vessels or cylinders, although
occasionally communicating with them,—these vessels I call condensers;
and whilst the engines are working, these condensers ought to be kept at
least as cold as the air in the neighbourhood of the engines by the application
of water or other cold bodies.—Thirdly. Whatever air or other
elastic vapour is not condensed by the cold of the condenser, and may
impede the working of the engine, is to be drawn out of the steam-vessels
or condensers by means of pumps, wrought by the engines themselves or
6otherwise.—Fourthly. I intend in many cases to employ the expansive
force of steam to press on the pistons, or whatever may be used instead of
them, in the same manner in which the pressure of the atmosphere is now
employed in common fire engines. In cases where cold water cannot be
had in plenty, the engines may be wrought by this force of steam only,
by discharging the steam into the air after it has done its office.—Lastly.
Instead of using water to render the pistons and other parts of the engines
air- and steam-tight, I employ oils, wax, resinous bodies, fat of animals,
quicksilver, and other metals in their fluid state.”
Fig. 4.—Governor and Throttle-Valve.
From the engraving we give of Watt’s double-action steam engine, Fig. 3,
and the following description, the reader will realize the high degree of perfection
to which the steam engine was brought by Watt. The steam is conveyed
to the cylinder through a pipe, B, the supply being regulated by the
throttle-valve, acted on by rods connected with the governor, D, which has a
rotary motion. This apparatus is designed to regulate the admission of
steam in such a manner that the speed of the engine shall be nearly uniform;
and the mode in which this is accomplished may be seen in Fig. 4,
where D D is a vertical axis carrying the pulley, d, which receives a rotary
motion from the driving-shaft of the engine, by a band not shown in the
figures. Near the top of the axis, at e, two bent rods work on a pin,
crossing each other in the same manner as the blades of a pair of scissors.
The two heavy balls are attached to the lower arms of these levers, which
move in slits through the curved guides intended to keep them always in
the same vertical plane as the axis, D D. The upper arms are jointed at f f
to rods hinged at h h to a ring not attached to the axis, but allowing it to
revolve freely within it. To this ring at F is fastened one end of the lever
connected with the throttle-valve in a manner sufficiently obvious from
7the cut. The position represented is that assumed by the apparatus when
the engine is in motion, the disc-valve, z, being partly open. If from any
cause the velocity of the engine increases, the balls diverge from increased
centrifugal force, and the effect is to draw down the ring at F, and, through
the system of levers, to turn the disc in the direction of the arrows, and
diminish the supply of steam. If, on the other hand, the speed of the
engine is checked, the balls fall towards the axis, and the valve is opened
wider, admitting steam more freely, and so restoring its former speed to the
engine. On one side of the cylinder are two hollow boxes, E E, Fig. 3, communicating
with the cylinder by an opening near the middle of the box.
Each of these steam-chests is divided into three compartments by conical
valves attached to rods connected with the lever, H. These valves are so
arranged that when the upper part of the cylinder is in communication
with the boiler, the lower part is open to the condenser, I, and vice versâ.
The top of the cylinder is covered, and the piston-rod passes through an
air and steam-tight hole in it; freedom of motion, with the necessary close
fitting, being attained by making the piston-rod pass through a stuffing-box,
where it is closely surrounded with greased tow. The piston is also packed,
so that, while it can slide freely up and down in the cylinder, it divides the
latter into two steam-tight chambers. In an engine of this kind, the elastic
force of the steam acts alternately on the upper and lower surfaces of the
piston; and the condenser, by removing the steam which has performed its
office, leaves a nearly empty space before the piston, in which it advances
with little or no resistance. On the rod which works the air-pump, two
pins are placed, so as to move the lever, H, up and down through a certain
space, when one pin is near its highest and the other near its lowest position,
and thus the valves are opened and closed when the piston reaches
the termination of its stroke. In the condenser, I, a stream of cold water
is constantly playing, the flow being regulated by the handle, f. The steam,
in condensing, heats the cold water, adding to its bulk, and at the same
time the air, which is always contained in water, is disengaged, owing to
the heat and the reduced pressure. Hence it is necessary to pump out
both the air and the water by the pump, J, which is worked by the beam
of the engine. In his engines Watt adopted the heavy fly-wheel, which
tends to equalize the movement, and render insensible the effects of those
variations in the driving power and in the resistance which always occur.
In the action of the engine itself there are two positions of the piston,
namely, where it is changing its direction, in which there is no force whatever
communicated to the piston-rod by the steam. These positions are
known as the “dead points,” and in a rotatory engine occur twice in each
revolution. The resistance also is liable to great variations. Suppose, for
example, that the engine is employed to move the shears by which thick
plates of iron are cut. When a plate has been cut, the resistance is removed,
and the speed of the engine increases; but this increase, instead of
taking place by a sudden start, takes place gradually, the power of the
engine being in the meantime absorbed in imparting increased velocity to
the fly-wheel. When another plate is put between the shears, the power
which the fly-wheel has gathered up is given out in the slight diminution
of its speed occasioned by the increased resistance. But for the fly-wheel,
such changes of velocity would take place with great suddenness, and the
shocks and strains thereby caused would soon injure the machine. This
expedient, in conjunction with that admirable contrivance, the “governor,”
renders it possible to set the same engine at one moment to forge an
8anchor, and at the next to shape a needle. One of the most ingenious of
Watt’s improvements is what is termed the “parallel motion,” consisting
of a system of jointed rods connecting the head of the piston-rod, R, with
the end of the oscillating beam. As, during the motion of the engine, the
former moves in a straight line, while the latter describes a circle, it would
be impossible to connect them directly. Watt accomplished this by
hinging rods together in form of a parallelogram, in such a manner that,
while three of the angles describe circles, the fourth moves in nearly a
straight line. Watt was himself surprised at the regularity of the action.
“When I saw it work for the first time, I felt truly all the pleasure of
novelty, as if I was examining the invention of another man.”
A B is half the beam, A being the main centre; B E, the main links, connecting the piston-rod, F, with the end of the beam; G D, the air-pump links, from the centre of which the air-pump-rod is suspended; C D moves about the fixed centre, C, while D E is movable about the centre D, itself moving in an arc, of which C is the centre. The dotted lines show the position of the links and bars when the beam is at its highest position.
Fig. 4a.—Watt’s Parallel Motion.
Many improvements in the details and fittings of almost every part of
the steam engine have been effected since Watt’s time. For example,
the opening and closing of the passages for the steam to enter and leave
the cylinder is commonly effected by means of the slide-valve (Fig. 5).
The steam first enters a box, in which are three holes placed one above
the other in the face of the box opposite to the pipe by which the steam
enters. The uppermost hole is in communication with the upper part of
the cylinder, and the lowest with the lower part. The middle opening
leads to the condenser, or to the pipe by which the steam escapes into the
air. A piece of metal, which may be compared to a box without a lid,
slides over the three holes with its open side towards them, and its size is
such that it can put the middle opening in communication with either the
uppermost or the lowest opening, at the same time giving free passage for
the steam into the cylinder by leaving the third opening uncovered. In A,
Fig. 5, the valve is admitting steam below the piston, which is moving
upwards, the steam which had before propelled it downwards now having
free exit. When the piston has arrived at the top of the cylinder, the slide
is pushed down by the rod connecting it with the eccentric into the position
represented at B, and then the opposite movement takes place. The
slide-valve is not moved, like the old pot-lid valves, against the pressure of
the steam, and has other advantages, amongst which may be named the
readiness with which a slight modification renders it available for using
the steam “expansively.” This expansive working was one of Watt’s inventions,
9but has been more largely applied in recent times. In this plan,
when the piston has performed a part of its stroke, the steam is shut off,
and the piston is then urged on by the expansive force of the steam enclosed
in the cylinder. Of course as the steam expands its pressure decreases; but
as the same quantity of steam performs a much larger amount of work
when used expansively, this plan of cutting off the steam is attended with
great economy. It is usually effected by the modification of the slide-valve,
shown at C, Fig. 5, where the faces of the slides are made of much greater
width than the openings. This excess of width is called the “lap,” and
by properly adjusting it, the opening into the cylinder may be kept closed
during the interval required, so that the steam is not allowed to enter the
cylinder after a certain length of the stroke has been performed. The
slide-valve is moved by an arrangement termed the eccentric. A circular
disc of metal is carried on the shaft of the engine, and revolves with it.
The axis of the shaft does not, however, run through the centre of the disc,
but towards one side. The disc is surrounded by a ring, to which it is not
attached, but is capable of turning round within it. The ring forms part
of a triangular frame to which is attached one arm of a lever that communicates
the motion to the rod bearing the slide. Expansive working is
often employed in conjunction with superheated steam, that is, steam heated
out of contact with water, after it has been formed, so as to raise its temperature
beyond that merely necessary to maintain it in the state of steam,
and to confer upon it the properties of a perfect gas. Experience has proved
that an increased efficiency is thus obtained.
Fig. 5.—Slide Valve.
The actual power of a steam engine is ascertained by an instrument called
the Indicator, which registers the amount of pressure exerted by the steam
on the face of the piston in every part of its motion. The indicator consists
simply of a very small cylinder, in which works a piston, very accurately
made, so as to move up and down with very little friction. The
piston is attached to a strong spiral spring, so that when the steam is
admitted into the cylinder of the indicator the spring is compressed, and
its elasticity resists the pressure of the steam, which tends to force the
piston up. When the pressure of steam below the piston of the indicator
10is equal to that of the atmosphere, the spring is neither compressed nor
extended; but when the steam-pressure falls below that of the atmosphere,
as it does while the steam is being condensed, then the atmospheric pressure
forces down the piston of the indicator until it is balanced by the
tension of the now stretched spring. The extension or compression of
the spring thus measures the difference between the pressure of the atmosphere
and that of the steam in the cylinder of the engine, with which the
cylinder of the indicator freely communicates.
From the piston-rod of the indicator a pencil projects horizontally, and
its point presses against a sheet of paper wound on a drum, which moves
about a vertical axis. This drum is made to move backwards and forwards
through a part of a revolution, so that its motion may exactly correspond
with that of the piston in the cylinder of the steam engine. Thus, if the
piston of the indicator were to remain stationary, a level line would be
traced on the paper by the movement of the drum; and if the latter did
not move, but the steam were admitted to the indicator, the pencil would
mark an upright straight line on the paper. The actual result is that a
figure bounded by curved lines is traced on the paper, and the curve accurately
represents the pressure of the steam at every point of the piston’s
motion. The position of the point of the pencil which corresponds with
each pound of pressure per square inch is found by trial by the maker of
the instrument, who attaches a scale to show what pressures of steam are
indicated.
If the pressure per square inch is known, it is plain that by multiplying
that pressure by the number of square inches in the area of the piston of
the engine, the total pressure on the piston can be found. The pressure
does not rise instantly when the steam is first admitted, nor does it fall
quite abruptly when the steam is cut off and communication opened with
the condenser. When the steam is worked expansively, the pressure falls
gradually from the time the steam is shut off. Now, the amount of work
done by any force is reckoned by the pressure it exerts multiplied into the
space through which that pressure is exerted. Therefore the work done
by the steam is known by multiplying the pressure in pounds on the whole
surface of the piston into the length in feet of the piston’s motion through
which that pressure is exerted. The trace of the pencil on the paper—i.e.,
the indicator diagram—shows the pressures, and also the length of the
piston’s path through which each pressure is exerted, and therefore it is
not difficult to calculate the actual work which is done by the steam at
every stroke of the engine. If this be multiplied by the number of strokes
per minute, and the product divided by 33,000, we obtain what is termed
the indicated horse-power of the engine. The work done per minute is
divided by 33,000, because that number is taken to represent the work that
a horse can do in a minute: that is, the average work done in one minute
by a horse would be equal to the raising of the weight of 1,000 lbs. thirty-three
feet high, or the raising of thirty-three pounds 1,000 feet high. The
number, 33,000, as expressing the work that could be done by a horse in
one minute, was fixed on by Watt, but more recent experiments have shown
that he over-estimated the power of horses, and that we should have to
reduce this number by about one-third if we desire to express the actual
average working power of a horse. But the power of engines having come
to be expressed by stating the horse-power on Watt’s standard, engineers
have kept to the original number, which is, however, to be considered as a
merely artificial unit or term of comparison between one engine and another;
11for the power of a horse to perform work will vary with the mode in
which its strength is exerted. The source of the power which does the
work in the steam engine is the combustion of the coal in the furnace under
the boiler. The amount of work a steam engine will do depends not only
on the quantity of steam which is generated in a given time, but also upon
the pressure, and therefore the temperature at which the steam is formed.
Fig. 6.—Section of Giffard’s Injector.
The water constantly evaporating in the boiler of a steam engine is
usually renewed by forcing water into the boiler against the pressure of
the steam by means of a small pump worked by the engine. In the engraving
of Watt’s engine this pump is shown at M. But recently the feed-pump
has been to a great extent superseded by a singular apparatus invented
by M. Giffard, and known as Giffard’s Injector. In this a jet of
steam from the boiler itself supplies the means of propelling a stream of
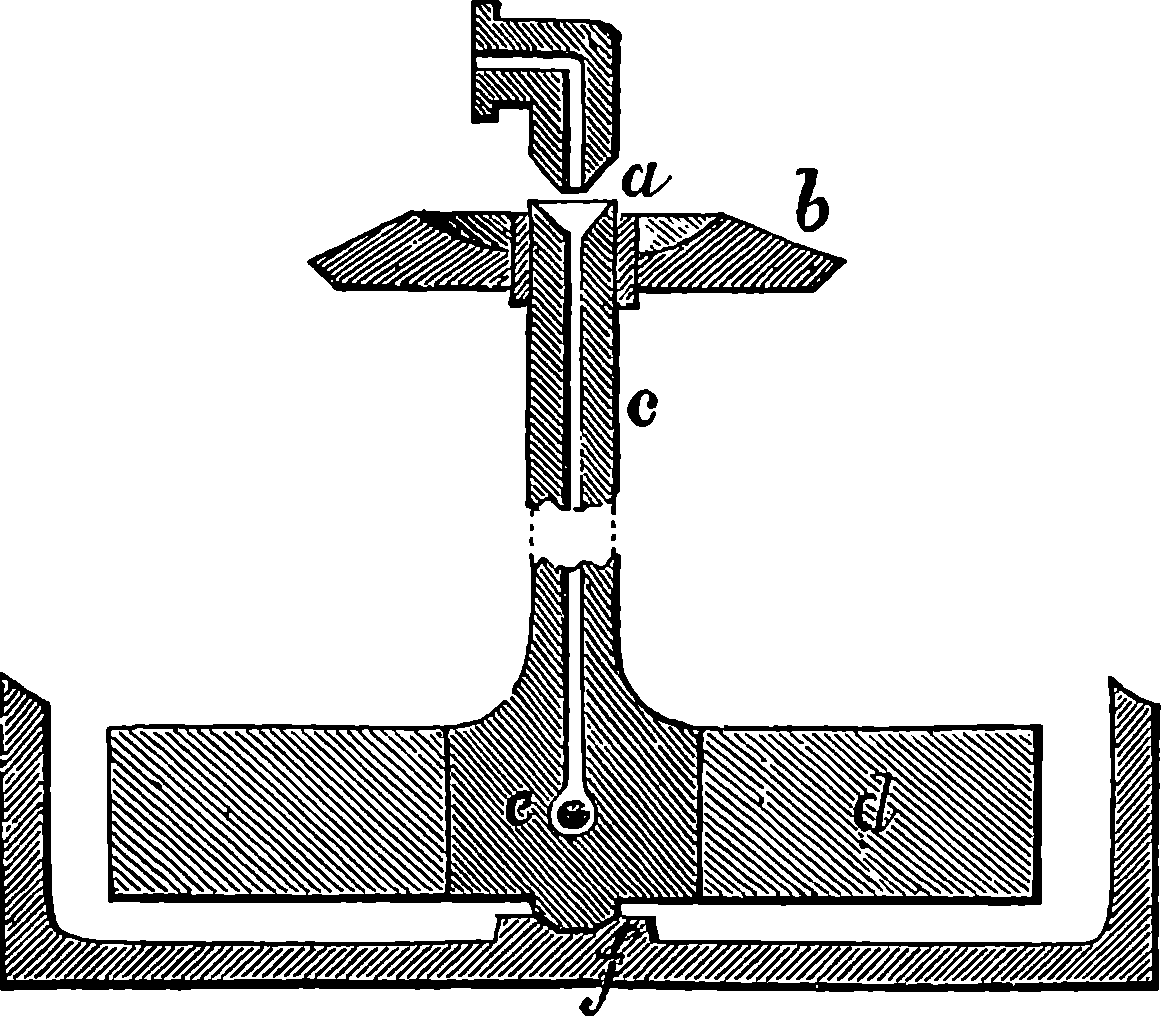
water directly into the boiler. Fig. 6 is a section of this interesting
apparatus through its centre, and it clearly shows the manner in which
the current of steam is made to operate on the jet of water. The steam
from the boiler passes through the pipe A and into the tube B through the
holes. The nozzle of this tube is of a conical shape, and its centre is occupied
by a rod pointed to fit into the conical nozzle, and provided with a
screw at the other end, so that the opening can be regulated by turning the
handle, C. At D the jet of steam comes in contact with the water which
feeds the boiler, the arrangement being such that the steam is driven into
the centre of the stream of water which enters by the pipe E, and is propelled
by the steam jet through another cone, F, issuing with such force
from the orifice of the latter that it is carried forward through the small
opening at G into the chamber H. Here the water presses on the valve K,
which it raises against the pressure of the steam and enters the boiler.
The water issuing from the cone, F, actually traverses an open space which is
exposed to the air, and where the fluid may be seen rushing into the boiler
as a clear jet, except a few beads of steam which may be carried forward
in the centre, the rest of the steam having been condensed by the cold
12water. The steam, of course, rushes from the cone, B D, with enormous
velocity, which is partly communicated to the water. The pipe, L, is for the
water which overflows in starting the apparatus, until the pressure in H becomes
great enough to open the valve. The supplies of water and of steam
have to be adjusted according to the conditions of pressure in the boiler,
and according to the temperature of the feed-water. It is found that when
the feed-water is at a temperature above 120° Fahrenheit, the injector will
not work: the condensation of the steam is therefore necessary to the
result. For, as the steam is continually condensed by the cold water,
it rushes from D with the same velocity as into a vacuum, and
the water is urged on by a momentum due to this velocity. We
must observe, moreover, that the net result of the operation is a lessening
of the pressure in the boiler; for the entrance of the feed-water produces
a fall of temperature in the boiler, and the bulk of steam expended is
fourteen times the bulk of the water injected: thus, although the apparatus
before actual trial would not appear likely to produce the required result,
the effect is no more paradoxical than in the case of the feed-pump. The
injector has been greatly improved by Mr. Gresham, who has contrived
to make some of the adjustments self-acting, and his form of the apparatus
is now largely used in this country. The injector is applicable to stationary,
locomotive, or marine engines.
Steam boilers are now always provided with one
of Bourdon’s gauges, for indicating the pressure of
the steam. The construction of the instrument
will easily be understood by an examination of
Fig. 7. The gauge is screwed into some part of
the boiler, where it can always be seen by the
person in charge. The stop-cock A communicates
with the curved metallic tube C, which is
the essential part of the contrivance. This tube
is of the flattened form shown at D, having its
greatest breadth perpendicular to the plane in
which the tube is curved, and it is closed at the
end E, where it is attached to the rod F, so that
any movement of E causes the axle carrying the
index-finger, F, to turn, and the index then moves
along the graduated arc. The connection is
sometimes made by wheelwork, instead of by the
simple plan shown in the figure. The front plate
is represented as partly broken away, in order to
show the internal arrangement, which, of course,
is not visible in the real instrument, where only
the index-finger and graduated scale are seen,
protected by a glass plate.
Fig. 7.—Bourdon’s Pressure Gauge.
When a curved tube of the shape here described is subjected to a greater
pressure on the inside than on the outside, it tends to become straighter,
and the end E moves outward; but when the pressure is removed, the
tube resumes its former shape. The graduations on the scale are made by
marking the position of the index when known pressures are applied. The
amounts of pressure, when the gauges are being graduated, are known by
the compression produced in air contained in another apparatus. Gauges
constructed on Bourdon’s principle are applied to other purposes, and can
be made strong enough to measure very great pressures, such as several
13thousand pounds on the square inch; they may also be made so delicate
as to measure variations of pressure below that of the atmosphere. The
simplicity and small size of these gauges, and the readiness with which
they can be attached, render them most convenient instruments wherever
the pressure of a gas or liquid is required to be known.
Fig. 8.—Steam Generator.
A point to which great attention has been directed of late years is the
construction of a boiler which shall secure the greatest possible economy
in fuel. Of the total heat which the fuel placed in the furnace is capable
of supplying by its combustion, part may be wasted by an incomplete
burning of the fuel, producing cinders or smoke or unburnt gases, another
part is always lost by radiation and conduction, and a third portion is
carried off by the hot gases that escape from the boiler-flues. Many contrivances
have been adopted to diminish as much as possible this waste
of heat, and so obtain the greatest possible proportion of available steam
power from a given weight of fuel. Boilers wholly or partially formed of
tubes have recently been much in favour. An arrangement for quickly
14generating and superheating steam is shown in Fig. 8, in connection with
a high-pressure engine.
Steam engines are constructed in a great variety of forms, adapted to
the purposes for which they are intended. Distinctions are made according
as the engine is fitted with a condenser or not. When steam of a low
pressure is employed, the engine always has a condenser, and as in this
way a larger quantity of work is obtainable for a given weight of fuel, all
marine engines—and all stationary engines, where there is an abundant
supply of water and the size is not objectionable—are provided with condensers.
High-pressure steam may be used with condensing engines, but
is generally employed in non-condensing engines only, as in locomotives
and agricultural engines, the steam being allowed to escape into the air
when it has driven the piston to the end of the stroke. In such engines
the beam is commonly dispensed with, the head of the piston-rod moving
between guides and driving the crank directly by means of a connecting-rod.
The axis of the cylinder may be either vertical, horizontal, or inclined.
A plan often adopted in marine engines, by which space is saved,
consists in jointing the piston-rod directly to the crank, and suspending
the cylinder on trunnions near the middle of its length. The trunnions are
hollow, and are connected by steam-tight joints, one with the steam-pipe
from the boiler, and the other with the eduction-pipe. Such engines have
fewer parts than any others; they are lighter for the same strength, and
are easily repaired. The trunnion joints are easily packed, so that no leakage
takes place, and yet there is so little friction that a man can with one
hand move a very large cylinder, whereas in another form of marine engine,
known as the side-lever engine, constructed with oscillating beams, the
friction is often very great.
The first locomotive came into practical use in 1804. Twenty years
before, Watt had patented—but had not constructed—a locomotive
engine, the application of steam to drive carriages having first been suggested
by Robinson in 1759. The first locomotives were very imperfect,
and could draw loads only by means of toothed driving-wheels, which
engaged teeth in rack-work rails. The teeth were very liable to break off,
and the rails to be torn up by the pull of the engine. In 1813, the important
discovery was made that such aids are unnecessary, for it was found
that the “bite” of a smooth wheel upon a smooth rail was sufficient for all
ordinary purposes of traction. But for this discovery, the locomotive might
never have emerged from the humble duty of slowly dragging coal-laden
waggons along the tramways of obscure collieries. The progress of the
locomotive in the path of improvement was, however, slow, until about
1825, when George Stephenson applied the blast-pipe, and a few years
later adopted the tubular boiler. These are the capital improvements
which, at the famous trial of locomotives, on the 6th of October, 1829,
enabled Stephenson’s “Rocket” to win the prize offered by the directors
of the Liverpool and Manchester Railway. The “Rocket” weighed 4½
tons, and at the trial drew a load of tenders and carriages weighing 12¾
tons. Its average speed was 14 miles an hour, and its greatest, 29 miles
15an hour. This engine, the parent of the powerful locomotives of the present
day, may now be seen in the Patent Museum at South Kensington.
Since 1829, numberless variations and improvements have been made in
16the details of the locomotive. In weight, dimensions, tractive power and
speed, the later locomotives vastly surpass the earlier types.
Fig. 9.—Section of Locomotive (A.D. 1837).
Fig. 9 represents the section of a locomotive constructed c. 1837. The
boiler is cylindrical; and at one end is placed the fire-box, partly enclosed
in the cylindrical boiler, and surrounded on all sides by the water, except
where the furnace door is placed, and at the bottom, where the fuel is
heaped up on bars which permit the cinders to drop out. At the other
end of the boiler, a space beneath the chimney called the smoke-box is
connected with the fire-box by a great number of brass pipes, open at
both ends, firmly fixed in the end plates of the boiler. These tubes are
from 1¼ in. to 2 in. in diameter, and are very numerous—usually about
one hundred and eighty, but sometimes nearly double that number. They
therefore present a large heating surface to the water, which stands at a
level high enough to cover them all and the top of the fire-box. The
boiler of the locomotive is not exposed to the air, which would, if allowed
to come in contact with it, carry off a large amount of heat. The outer
surface is therefore protected from this cooling effect by covering it with
a substance which does not permit the heat to readily pass through it.
Nothing is found to answer better than felt; and the boiler is accordingly
covered with a thick layer of this substance, over which is placed a layer
of strips of wood ¾ in. thick, and the whole is surrounded with thin sheet
iron. It is this sheet iron alone that is visible on the outside. The level
of the water in the boiler is indicated by a gauge, which is merely a very
strong glass tube; and the water carried in the tender is forced in as
required, by a pump (not shown in the Fig.). The steam leaves the boiler
from the upper part of the steam-dome, A, where it enters the pipe, B; the
object being to prevent water from passing over with the steam into the
pipe. The steam passes through the regulator, C, which can be closed or
opened to any extent required by the handle, D, and rushes along the pipe,
E, which is wholly within the boiler, but divides into two branches when
it reaches the smoke-box, in order to conduct the steam to the cylinders.
Of these there are two, one on each side, each having a slide-valve, by
means of which the steam is admitted before and behind the pistons alternately,
and escapes through the blast-pipe, F, up the chimney, G, increasing
the draught of the fire by drawing the flame through the longitudinal tubes
in proportion to the rush of steam; and thus the rate of consumption of
fuel adjusts itself to the work the engine is performing, even when the
loads and speeds are very different. Though the plane of section passing
through the centre of boiler would not cut the cylinders, one of them is
shown in section. H is the piston; K the connecting-rod jointed to the
crank, L, the latter being formed by forging the axle with four rectangular
angles, thus, ; and the crank bendings for the two cylinders are
placed in planes at right angles to each other, so that when one is at the
“dead point,” the other is in a position to receive the full power of the
piston. There are two safety valves, one at M, the other at N; the latter
being shut up so that it cannot be tampered with.
Locomotives are fitted with an ingenious apparatus for reversing the
engines, which was first adopted by the younger Stephenson, and is
known as the “link motion.” The same arrangement is employed in other
engines in which the direction of rotation has to be changed; and it serves
another important purpose, namely, to provide a means by which steam
may be employed expansively at pleasure. The link motion is represented
in Fig. 10, where A, B, are two eccentrics oppositely placed on the driving-shaft,
17and their rods joined to the ends of the curved bar or link, C D. A
slit extends nearly the whole length of this bar, and in it works the stud E,
forming part of the lever, F, G, movable about the fixed joint, G, and having
its extremity, F, jointed to the rod H, that moves the slide-valve. The weight
of the link and the eccentric rods is counterpoised with a weight, K, attached
to the lever, I K, which turns on the fixed centre, L. This lever
forms one piece with another lever, L M, with which it may be turned by
pulling the handle of O P, connected with it through the system of jointed
rods. When the link is lowered, as shown in the figure, the slide-valve
rod will follow the movement of the eccentric, B, while the backward and
forward movement of the other eccentric will only be communicated to
the end of C, and will scarcely affect the position of the stud E at all. By
drawing the link up to its highest position, the motion due to eccentric A
only will be communicated to the slide-valve rod, which will therefore be
drawn back at the part of the revolution where before it was pushed forward,
and vice versâ; hence the engine will be reversed. When the link
is so placed that the stud is exactly in the centre, the slide-valve will receive
no motion, and remain in its middle position, consequently the
engine is stopped. By keeping the link nearer or farther from its central
position, the throw of the slide-valve will be shorter or longer, and the
steam will be shut off from entering the cylinder when a smaller or larger
portion of the stroke has been performed.
Fig. 10.—Stephenson’s Link Motion.
18Although Fig. 9 represents with sufficient clearness all the essential
parts of a locomotive, it should be observed that as actually constructed
for use on the different lines of railway the machine is greatly modified
in the arrangement and proportions of its parts. A greater number of
adjuncts and subsidiary appliances are also provided for the more effective
and convenient working of the engine, and for giving control over the
movement of the train, and these, in fact, conduce much to the greater
economy and safety with which trains are now run. As the circumstances
and conditions under which railways are worked vary much in different
parts of the world, the locomotive has to be designed to meet the requirements
of each case, and its general appearance, details and dimensions
are accordingly much diversified. From among the many types of recent
locomotives we select for illustration and a short description the form of
express passenger engine that has lately been designed by Mr. T. W.
Worsdell, the engineer of the North Eastern Railway, and this will give
the opportunity of noticing some of the newest improvements, which are
embodied in this engine. See Plate II.
The plan of causing the steam to work expansively has already been
mentioned on pages 8 and 9, as used by cutting off the steam when part
of the stroke of the piston has been made. Another mode by which the
expansive principle has long been made use of in stationary and marine
engines is to allow the steam from the boiler to enter first a smaller
cylinder and from that, at the end of the stroke, to pass into a larger one
in which, as it expands, it exercises a diminished pressure. This arrangement
has been called the compound or double-cylinder engine, and was
known to possess certain advantages where high pressure steam was
made use of. Indeed, in marine engines the principle of “triple expansion”
is now quite commonly adopted—that is, the steam passes successively
into three cylinders of successively greater diameter. Mr. Webb,
the locomotive engineer of the London and North Western Railway,
appears to have been the first to make the “compounding” system a
practical success as applied to the locomotive. In Mr. Webb’s arrangement
there are three cylinders, two smaller ones for the high-pressure
steam from the boiler, and between these a single large low-pressure
cylinder which receives the steam that has done its work from both the
smaller cylinders. In Mr. Worsdell’s engine the original and simpler
locomotive construction of two cylinders has been adhered to, and thus
the general plan of the engine is unchanged except in the larger size of
the low-pressure cylinder. In the present engine the stroke is 24 in.; the
high-pressure cylinder has its internal diameter 20 in. and the low-pressure
cylinder a diameter of 28 in. The boiler-shell is made of steel,
the fire-box is of copper, and there are 203 brass tubes, 1¾ in. diameter
and 10 ft. 11 in. long, connecting the fire-box with the smoke-box. The
frame, and indeed most parts of the engine, are also made of steel. The
driving-wheels, which here are a single pair, have a diameter of 7 ft. 7¼ in.
The total “wheel-base” is nearly 21 ft., and it will be observed that the
forepart of the engine is supported on a four-wheeled bogie. The bogie is
capable of a certain amount of horizontal motion by turning round a
swivel, but this movement is controlled by springs, so that, notwithstanding
the length of the frame, the engine is enabled to take curves with great
facility, while its motion is perfectly steady even at the highest speeds.
The working pressure of the steam in the boiler is 170 lbs. on the square
inch. The steam which leaves the high-pressure cylinder is conveyed to
19the low-pressure cylinder by a pipe that is led round the inside of the
smoke-box, and thus enters the larger cylinder after taking up heat that
would otherwise be wasted, so that its elastic force is fully maintained.
This circumstance, no doubt, contributes to the very marked economy of
fuel that has been effected by the compound engines. How great the
economy is found in the working will be seen by the following results,
which are taken from the actual records. The same train was taken over
the same rails in ordinary quick passenger traffic for several journeys
which, as performed in the same time by the compound engine and by
another otherwise similar non-compound engine, required for the compound,
25,254 lbs. of coal; for the non-compound, 32,104 lbs.; or, the
consumption of coal by the former was 28 lbs. per mile; by the latter,
36 lbs. per mile. This represents a saving of about 21 per cent. of the
fuel. As the steam enters the high-pressure cylinder first, it would not
be possible to start the engine if it had stopped at one of the “dead-points”
on that side, without a special arrangement for admitting the
steam directly to the other cylinder in such cases. This, of course,
is required only for the first stroke, and Mr. Worsdell and M. von
Borries have contrived for this purpose an ingenious valve, brought into
operation when required by a touch from the engineer, and then immediately
adjusting itself automatically, so as to restore the steam connections
to their normal condition.
PLATE II.
NORTH EASTERN RAILWAY LOCOMOTIVE.
Fig. 10a.—G.N.R. Express Passenger Locomotive.
Another type of the high-speed passenger engines used for express
trains on several of the great English railways is well represented by one
of the Great Northern Company’s locomotives, as depicted in Fig. 10a.
In this there are a single pair of driving wheels of very large diameter,
namely, 8 ft. 2 in., so that each complete movement of the pistons will carry
the engine forwards a length of nearly 26 ft. There are outside cylinders,
and therefore the driving axle is straight, and the leading wheels are in
two pairs, mounted on a bogie which is capable of a certain amount of
independent horizontal rotation.
The Stephenson’s link motion, described on page 17, has lately been
often supplanted by another arrangement known as Joy’s valve gear,
which leaves the crank axle unencumbered with eccentrics, and, as taking
up less space, is generally now preferred for locomotives and also for
marine engines. Its principle is very simple, and will be readily understood
from the diagram in Fig. 10b, where c is the spindle of the slide-valves
20as in Fig. 5, but capable, we shall now suppose, of a horizontal
movement only. Jointed to it at D is a rod D E attached to a block at E,
which can move only within a slot in the strong bar E F in a circular
segment, the centre of which is at D. The bar we suppose for the moment
to be immovable, and disposed symmetrically to C D. Now let an alternate
up and down motion along the circular segment be given to block E,
and the effect will be to leave the centre, D, unchanged in position, and,
therefore, in that case the valve will not be moved at all. Now this
reciprocating movement is given to the block E by a system of levers
(not here shown), jointed to the connecting-rod (K, Fig. 9) in such a
manner that the rod D E is compelled to follow the movement of the
connecting-rod, but the end E must always travel in the circular segment.
We have hitherto supposed this segmental piece to be fixed, but the
engineer has the power of so turning it as to tilt either the upper or lower
part towards D. If, for instance, the guiding segment is fixed as at
II, the block in rising will push in the valve-spindle, and in descending
draw it out, as the length of the rod D E is invariable. But if the guides
be turned over so as to bring F nearer D than E, the same movement
of the block will give the reverse motions to the valve-spindle.
Fig. 10b.—Joy’s Valve Gear.
From the great rapidity with which the machinery of the locomotive
moves, the different parts require to be carefully balanced in order to prevent
dangerous oscillations. For example, the centrifugal force of the
massive cranks, etc., is balanced by inserting between the spokes of the
driving wheels certain counterpoises, the weights and positions of which
are finally adjusted by trial. The engine is suspended by chains and set
in motion, and a pencil attached to one corner of the frame marks on a
horizontal card the form of the oscillation, usually by an oval figure. When
the diameter of this figure is reduced to about 1 16 inch, the adjustment is
considered complete.
21The power of a locomotive, of course, depends on the pressure of the
steam and the size of the cylinder, &c.; but a very much lower limit than
is imposed by these conditions is set to the power of the engine to draw
loads by the adhesion between the driving wheels and the rails. By the
term “adhesion,” which is commonly used in this case, nothing more is
really meant than the friction between surfaces of iron. When the resistance
of the load drawn is greater than this friction, the wheels turn round
and slip on the rails without advancing. The adhesion depends upon the
pressure between the surfaces, and upon their condition. It is greater in
proportion as the weight supported by the driving-wheels is greater, and
when the rails are clean and dry it is equal to from 15 to 20 per cent. of
that part of the weight of the engine which rests on the driving-wheels;
but when the rails are moist, or, as it is called, “greasy,” the tractive
power may be only 5 per cent. of the weight; about one-tenth may be
taken as an average. Suppose that 30 tons of the weight of a locomotive
are supported by the driving-wheels, that locomotive could not be
employed to drag a train of which the resistance would cause a greater
pull upon the coupling-links of the tender than they would be subject to if
they were used to suspend a weight of 3 tons. The number of pairs of
wheels in a locomotive varies from two to five; most commonly there are
three pairs; and one, two, or all, are driven by the engine, the wheels
being coupled accordingly; very often two pairs are coupled.
The pressure at which the steam is used in the locomotive is sometimes
very considerable. A pressure equal to 180 lbs. on each square inch of the
surface of the boiler is quite usual. The greater economy obtained by
the employment of high-pressure steam acting expansively in the cylinder,
points to the probability of much higher pressures being adopted. There
is practically no limit but the power of the materials to resist enormous
strains, and there is no reason, in the nature of things, why steam of even
500 lbs. per square inch should not be employed, if it were found otherwise
desirable. It need hardly be said that locomotives are invariably constructed
of the very best materials, and with workmanship of the most
perfect kind. The boilers are always tested, by hydraulic pressure, to
several times the amount of the highest pressure the steam is required to
have, and great care is bestowed upon the construction of the safety-valves,
so that the steam may blow off when the due amount of pressure
is exceeded. The explosion of a locomotive is, considering the number of
engines in constant use, a very rare occurrence, and is probably in all
cases owing to the sudden generation of a large quantity of steam, and
not to an excessive pressure produced gradually. Among the causes
capable of producing explosive generation of steam may be mentioned the
deposition of a hard crust of stony matter, derived from the water; this
crust allows the boiler to be over-heated, and if water should then find its
way into contact with the heated metal, a large quantity of steam will be
abruptly generated. Or should the water in the boiler become too low,
parts of the boiler may become so heated that on the admission of fresh
water it would be suddenly converted into steam. When an explosion
does take place, the enormous force of the agent we are dealing with when
we bottle up steam in an iron vessel, is shown by the effects produced.
Fig. 11 is from a photograph taken from an exploded locomotive, where
we may see how the thick plates of iron have been torn like paper, and
the tubes, rods, and levers of the engine twisted in inextricable confusion.
Fig. 11.—Locomotive after Explosion.
Fig. 12.—Hancock’s Steam Omnibus.
Locomotive engines for propelling carriages on common roads were
22invented many years ago, by Gurney, Anderson, Scott Russell, Hancock,
and others. One designed by Hancock is represented in Fig. 12. Such
engines do not appear to have found much favour, though the idea has
been successfully realized in the traction engines lately introduced. Probably
the application of steam power to the propulsion of vehicles along
common roads fell into neglect on account of the superior advantages of
railways, but the common road locomotive is at present receiving some
attention. In the tramways which are now laid along the main roads in
most large cities we see one-half of the problem solved. It is not so much
mechanical difficulties that stand in the way of this economical system of
23locomotion, as the prejudices and interests which have always to be overcome
before the world can profit by new inventions. The engines can be
made noiseless, emitting no visible steam or smoke, and they are under
more perfect control than horses. But vestries and parochial authorities
offer such objections as that horses would be frightened in the streets, if
the engine made a noise; and if it did not, people would be liable to be
run over, and the horses be as much startled as in the other case. But
horses would soon become accustomed to the sight of a carriage moving
without equine aid, however startling the matter might appear to them at
first; and the objection urged against the noiseless engines might be
alleged against wooden pavements, india-rubber tires, and many other
improvements. It is highly probable that in the course of a few years the
general adoption of steam-propelled vehicles will displace horses, at least
upon tramways. The slowness with which inventions of undeniable utility
and of proved advantage come into general use may be illustrated by the
fact of some great English towns and centres of engineering industry not
having made a single tramway until, in all the populous cities of the
United States, and in almost every European capital, tramways had been
in successful operation for many years. [1890.]
Some time has elapsed since the foregoing paragraph was written for
an earlier edition of this work, and during that period there has been an
advance in both practice and opinion; so that now it has become highly
probable that before the century ends a great change may be witnessed in
our modes of locomotion, even on ordinary roads. Already every town
of importance throughout the United Kingdom has been provided with
excellent tramways, along which, in not a few instances, horseless vehicles
roll smoothly, to the great convenience of the general public, while not
one of the difficulties and dangers to general street traffic has been experienced
that were so confidently predicted by those who were unable to
perceive that an innovation might be an improvement. The now universally-popular
bicycle has been continually receiving improvements, of
which there appears to be no end, and as the machine and all the contrivances
connected with it are so familiar to everyone, there is no need
here to do more than to refer to them, because they have led the way to
great improvements in ordinary carriages.
The steam-propelled vehicle for common roads has just been mentioned
as an invention belonging to the first half of the century, and the reasons
it did not find favour have been alluded to. There exists in the United
Kingdom a law concerning horseless carriages travelling on highways,
which was passed to apply to traction engines, and enacts that other than
horse vehicles are not to go along a road at a greater speed than four
miles an hour, and only two miles an hour through a town, and moreover
they are to be preceded by a man bearing a red flag, etc. But a bill has
been introduced (1895) into the legislature to amend this law, and permit
the British people to use on their common roads such light self-propelled
carriages as are becoming popular in France, as may be seen from the
following account:—
On Tuesday, 11th June, 1895, a race was started from Versailles to
Bordeaux and back, a distance of 727 miles or more for the double
journey. The first prize was the substantial sum of 40,000 francs (£1,600),
to which was attached the condition of the carriage seating four persons,
and other prizes were also to be awarded to various kinds of automatic
vehicles. No fewer than sixty-six vehicles were entered for competition,
24and these were variously supplied with motive power from steam, electricity,
or petroleum spirit. The starting place was Versailles at 12·9
p.m., and at 10·32 on Wednesday morning MM. Panhard & Levassor’s
petroleum carriage arrived at Bordeaux, whence, after a stop of only four
minutes, the return journey was begun, but shortly afterward an accident
caused a delay of one hour, but the carriage made the whole distance at
the average of 14·9 miles per hour. In this and three other carriages
belonging to the same firm, the propeller was the Daimler motor.
Though this carriage was the first to accomplish the trip it received only
the second prize, the condition of seating four persons not having been
complied with. The first prize fell to a four-seated vehicle by Les Fils de
Peugeot Frères, a firm who carried off besides the third and fourth prizes.
These carriages were also driven by so-called petroleum motors. These
motors are really gas engines on the principle to be presently mentioned,
but the gas is produced by the vapourisation of a volatile constituent of
petroleum (benzoline). The Daimler motor is a compact combination of
two cylinders connected with a chamber containing the explosive mixture
of gas and air. The pistons perform their in and out strokes simultaneously,
but their working strokes alternately.
The application of steam power to agricultural operations has led to
the construction of engines specially adapted by their simplicity
and portability for the end in view. The movable agricultural engines
have, like the locomotives, a fire-box nearly surrounded by the water, and
horizontal tubes, and are set on wheels, so that they may be drawn by
horses from place to place. There is usually one cylinder placed horizontally
on the top of the boiler; and the piston-rod, working in guides,
is, as in the old locomotive, attached by a connecting-rod to the crank of
a shaft, which carries a fly-wheel, eccentrics, and pulleys for belts to communicate
the motion to the machines. Engines of this kind are also much
used by contractors, for hoisting stones, mixing mortar, &c. These engines
are made with endless diversities of details, though in most such simplicity
of arrangement is secured, that a labourer of ordinary intelligence may,
after a little instruction, be trusted with the charge of the engine; while
their economy of fuel, efficiency, and cheapness are not exceeded in any
other class of steam engine.
Besides the steam engines already described or alluded to, there are
many interesting forms of the direct application of steam power. There
are, for example, the steam roller and the steam fire-engine. The former
is a kind of heavy locomotive, moving on ponderous rollers, which support
the greater part of the weight of the engine. When this machine is made
to pass slowly over roads newly laid with broken stones, a few repetitions
of the process suffice to crush down the stones and consolidate the materials,
so as at once to form a smooth road. Steam power is applied to the
fire engine, not to propel it through the streets, but to work the pumps
which force up the water. The boilers of these engines are so arranged
that in a few minutes a pressure of steam can be obtained sufficient to
throw an effective jet of water. The cut at the end of this chapter represents
25a very efficient engine of this kind, which will throw a jet 200 feet
high, delivering 1,100 gallons of water per minute. It has two steam
cylinders and two pumps, each making a stroke of two feet. These are
placed horizontally, the pumps and the air reservoir occupying the front
part of the engine, while the vertical boiler is placed behind. The steam
cylinders, which are partly hid in the cut by the iron frame of the engine,
are not attached to the boiler, which by this arrangement is saved from
injurious strains produced by the action of the moving parts of the
mechanism. There are seats for eight firemen, underneath which is a
space where the hose is carried. A first-class steam fire-engine of this
kind, completely fitted, costs upwards of £1,300.
A cheap and very convenient prime mover has lately come into use, which
has certain advantages over even the steam engine. Where a moderate
or a very small power is required, especially where it is used only at
intervals, the gas engine is found to be more convenient. It is small and
compact, no boiler or furnace is required, and it can be started at any
moment. As now made, it works smoothly and without noise. The
piston is impelled, not by the expansive force of steam, but by that of
heated air, the heat being generated by the explosion of a mixture of
common coal gas and air within the cylinder itself. Thus a series of
small explosions has the same effect as the admissions of steam through a
valve. A due quantity of gas and air is introduced into the cylinder, and
is ignited by the momentary opening of a communication with a lighted
gas jet outside. But the machine is provided with a regulator or
governor, which so acts on the valve mechanism that this communication
is made at each stroke only when the speed of rotation falls below a
certain assigned limit, and thus the number of the explosions is less than
the number of strokes, unless its work absorbs the machine’s whole
energy, which, according to the size of the engine, may be from that of a
child up to 30–horse power.
Before the invention of the steam hammer, large forge hammers had
been in use actuated by steam, but in an indirect manner, the hammer
having been lifted by cams and other expedients, which rendered the
apparatus cumbersome, costly, and very wasteful of power, on account
of the indirect way in which the original source of the force, namely, the
pressure of the steam, had to reach its point of application by giving
the blow to the hammer. Not only did the necessary mechanism for
communicating the force in this roundabout manner interfere with the
space necessary for the proper handling of the article to be forged, but
the range of the fall of the hammer being only about 18 in., caused a very
rapid decrease in the energy of the blow when only a very moderate-sized
piece of iron was introduced. For example, a piece of iron 9 in. in diameter
reduced the fall of the mass forming the hammer to one-half, and
the work it could accomplish was diminished in like proportion. Besides,
as the hammer was attached to a lever working on a centre, the striking
face of the hammer was parallel to the anvil only at one particular point
of its fall; and again, as the hammer was always necessarily raised to the
same height at each stroke, there was absolutely no means of controlling
26the force of the blow. When we reflect on the fact that the rectilinear
motion of the piston in the cylinder of the engine had first to be converted
into a rotary one, by beams, connecting-rod, crank, &c., and then this
rotary movement transformed into a lifting one by the intervention of
wheels, shafts, cams, &c., while all that is required in the hammer is a
straight up-and-down movement, the wonder is that such an indirect and
cumbersome application of power should have for so many years been
contentedly used. But in November, 1839, Mr. Nasmyth, an eminent
engineer of Manchester, received a letter from a correspondent, informing
him of the difficulty he had found in carrying out an order received for
the forging of a shaft for the paddle-wheels of a steamer, which shaft was
required to be 3 ft. in diameter. There was in all England no forge hammer
capable of executing such a piece of work. This caused Mr. Nasmyth
to reflect on the construction of forge hammers, and in a few minutes he
had formed the conception of the steam hammer. He immediately sketched
the design, and soon afterward the steam hammer was a fait accompli, for
Mr. Nasmyth had one at once executed and erected at his works, where
he invited all concerned to come and witness its performances. Will it
be believed that four years elapsed before this admirable application of
steam power found employment outside the walls of Mr. Nasmyth’s workshops?
After a time he succeeded in making those best able to profit
by such an invention aware of the new power—for such it has practically
proved itself, having done more to revolutionize the manufacture of iron
than any other inventions that can be named, except, perhaps, those of
Cort and Bessemer. The usual prejudice attending the introduction of
any new machine, however obvious its advantages are afterward admitted
to be, at length cleared away, and the steam hammer is from henceforth
an absolute necessity in every engineering workshop, and scarcely less so
for some of the early stages of the process of manufacturing crude wrought
iron. Whether blows of enormous energy or gentle taps are required, or
strokes of every gradation and in any order, the steam hammer is ready
to supply them.
Fig. 13.—Nasmyth’s Steam Hammer.
A steam hammer of the smaller kind is represented in Fig. 13. The
general mode of action will easily be understood. The steam is admitted
below the piston, which is thus raised to any required height within the
limits of the stroke. When the communication with the boiler is shut off
and the steam below the piston is allowed to escape, the piston, with the
mass of iron forming the hammer attached to the piston-rod, falls by its
own weight. This weight, in the large steam hammers, amounts to several
tons; and the force of the blow will depend jointly upon the weight of the
hammer, and upon the height from which it is allowed to fall. The steam
is admitted and allowed to escape by valves, moved by a lever under the
control of a workman. By allowing the hammer to be raised to a greater
or less height, and by regulating the escape of the steam from beneath the
piston, the operator has it in his power to vary the force of the blow. Men
who are accustomed to work the valves can do this with great nicety.
They sometimes exhibit their perfect control over the machine by cracking
a nut on the anvil of a huge hammer; or a watch having been placed—face
upwards—upon the anvil, and a moistened wafer laid on the glass, a
practised operator will bring down the ponderous mass with such exactitude
and delicacy that it will pick up the wafer, and the watch-glass will not even
be cracked. The steam hammer has recently been improved in several
ways, and its power has been more than doubled, by causing the steam,
27during the descent, to enter above the piston and add its pressure to the
force of gravity. Probably one of the most powerful steam hammers ever
constructed is that recently erected at the Royal Gun Factory at Woolwich,
for the purpose of forging great guns for the British Navy. It has
been made by Nasmyth & Co., and is in shape similar to their other steam
hammers. Its height is upwards of 50 ft., and it is surrounded with furnaces
and powerful cranes, carrying the huge iron tongs that are to grasp
the glowing masses. The hammer descends not merely with its own weight
of 30 tons; steam is injected behind the falling piston, which is thus driven
down with vastly enhanced rapidity and impulse. Of the lower portion of
this stupendous forge, nothing is visible but a flat table of iron—the anvil—level
with the floor of the foundry. But more wonderful, perhaps, than
anything seen aboveground, is the extraordinarily solid foundation beneath.
Huge tablets of foot-thick castings alternate with concrete and enormous
baulks of timber, and, lower down, beds of concrete, and piles driven
deep into the solid earth, form a support for the uppermost plate, upon
which the giant delivers his terrible stroke. Less than this would render
it unsafe to work the hammer to its full power. As the monster works—soberly
28and obediently though he does it—the solid soil trembles, and
everything movable shivers, far and near, as, with a scream of the steam,
our ‘hammer of Thor’ came thundering down, mashing the hot iron into
shape as easily as if it were crimson dough, squirting jets of scarlet and
yellow yeast. The head of the hammer, which of course works vertically,
is detachable, so that if the monster breaks his steel fist upon coil or anvil,
another can be quickly supplied. These huge heads alone are as big as a
sugar-hogshead, and come down upon the hot iron with an energy of more
than a thousand foot-tons. By the courteous permission of Major E.
Maitland, Superintendent of the Royal Gun Factories, we are enabled to
present our readers with the view of the monster hammer which forms the
Plate III.
Mr. Condie, in his form of steam hammer, utilizes the mass of the cylinder
itself to serve as the hammer. The piston-rod is hollow, and forms a pipe,
through which the steam is admitted and discharged, and the piston is stationary,
the cylinder moving instead—between vertical guides. A hammer
face is attached to the bottom of the cylinder by a kind of dovetail socket,
so that if the striking surface becomes injured in any way, another can
easily be substituted. The massive framework which supports the moving
parts of Condie’s hammer has its supports placed very far apart, so as to
leave ample space for the handling of large forgings.
Fig. 14.—Merryweather’s Steam Fire-Engine.
PLATE III.
THE GREAT STEAM HAMMER, ROYAL GUN FACTORY, WOOLWICH.
29
Fig. 15.—A Foundry.
IRON. — IRON IN ARCHITECTURE. — Tall Buildings in American Cities. — BIG WHEELS.
“Iron and coal,” it has been well said, “are kings of the earth”; and this
is true to such an extent that there is scarcely an invention claiming
the reader’s attention in this book but what involves the indispensable
use of these materials. Again, in their production on the large scale it
will be seen that there is a mutual dependence, and that this is made
possible only by means of the invention we have begun with; for without
the steam engine the deep coal mines could not have the water pumped
out of them,—it was indeed for this very purpose that the steam engine
was originally contrived,—nor could the coal be efficiently raised without
steam power. Before the steam engine came into use iron could not be
produced or worked to anything like the extent attained even in the
middle of the nineteenth century, for only by steam power could the blast
be made effective and the rolling mill do its work. On the other hand,
the steam engine required iron for its own construction, and this at once
caused a notable increase in the demand for the metal. Once more, the
engine itself supplies no force; for without the fuel which raises steam
from the water in the boiler it is motionless and powerless, and that fuel
is practically coal. In consequence of thus providing power, and also of
supplying a requisite for the production of iron, coal has acquired
supreme industrial importance, so that all our great trades and places of
30densest population are situated in or near coal-fields. But what we
have further to say about coal may be conveniently deferred to a
subsequent article, while we proceed to treat of iron, and of the contrivances
in which it plays an essential part.
Iron has also been called “the mainspring of civilization,” and the
significance of the phrase is obvious enough when we consider the
enormous number and infinite variety of the things that are made of it:
the sword and the ploughshare; all our weapons of war and all our
implements of peace; the slender needle and the girders that span wide
rivers; the delicate hair-spring of the tiny watch and the most tenacious
of cables; the common utensils of domestic life and the huge battle-ships
of our fleets; the smoothest roads, the loftiest towers, the most
spacious pleasure palaces. Such extensive applications of iron for
purposes so diverse have been rendered possible only by the greater
facility and cheapness of production, together with the better knowledge
of the properties of the substance and increased skill in its treatment, that
have particularly distinguished our century. Apart again from the
constructive uses of iron, it enters essentially into another class of inventions
of which the age is justly proud, namely, those which utilize
electricity in the production of light, mechanical power, and chemical
action; for it is on a quality possessed by iron, and by iron alone, that
the generation of current by the electric dynamo ultimately depends.
This peculiar property of iron, which was first announced by Arago in
1820, and has since proved so fertile in practical applications, is that a
bar of the metal can, under suitable conditions, be instantly converted
into the most powerful of magnets, and as quickly demagnetized. What
these conditions are will be explained when we come to treat of
electricity.
Fig. 16.—Aerolite in the British Museum.
Besides the unique property of iron just referred to, and its superlative
utility in arts and industries, there are other circumstances that
give a peculiar interest to this metal. It is the chief constituent of many
minerals, and traces or small quantities are found in most of the materials
that make up the crust of the earth; it is present also in the organic
kingdoms, being especially notable in the blood of vertebrate (back-boned)
animals, of which it is an essential component. Notwithstanding its
wide diffusion, iron is not found native, that is, as metal, but has to be
extracted from its ores, which are usually dull stony-looking substances,
as unlike the metal as can be conceived. In this respect it differs from
gold, which is not met in any other than the metallic state, in the form of
nuggets, minute crystals or branching filaments, and from metals such as
silver, copper, and a few others which also are occasionally found native.
It is true that rarely small quantities of metallic iron have been met with
in the form of minute grains disseminated in volcanic rocks; but in
contrast with the practical absence of metallic iron from terrestrial
accessible materials is the fact that masses of iron, sometimes of nearly
pure metal, occasionally descend upon the earth from interplanetary
space. These are aerolites, of which there are several varieties, some
consisting only of crystalline minerals without any metallic iron, others of
a mixture of minerals and metals, but the most common are of iron,
always alloyed with a small quantity of nickel, and usually containing
also traces more or less of a few other metals and known chemical
elements. The iron in some specimens has been found to amount to 93
per cent. of the whole. These aerolites, or meteorites, as they are also
31called, are of irregular shape and vary greatly in size, which however is
sometimes very considerable: one found in South America was calculated
to weigh 14 tons, another discovered in Mexico, 20 tons. There is in the
British Museum a good specimen of an iron meteorite, which is
represented in Fig. 16, where it will be observed that a portion has been
cut off to form a plane surface, which when polished and etched by an
acid, reveals a crystalline structure quite peculiar and distinctive, so that
such meteorites can be recognized with certainty, even if they did not
possess surface characters which are easily observed and identified when
once a specimen has been examined. The fall of meteorites to the
surface of the earth is comparatively rare, but it has been witnessed by
even scientific observers; as when Gassendi, the French astronomer,
saw in Provence the fall of a meteorite weighing 59 lbs. In the Transactions
of the Royal Society for 1802 may be found a detailed account of
an instance in England of the fall which took place in Yorkshire, on the
13th December 1795, of a stone 56 lbs. in weight. Aerolites become
ignited or incandescent by reason of the great velocity with which they
32pass through the atmosphere, whereby the air in front of them is condensed
and heated, the heat often being sufficient to liquefy or even
vaporize the solid matter. The so-called shooting stars are with good
reason believed to be nothing but such incandescent aerolites, and the
aerolites themselves are regarded as small asteroids, or scattered planetary
dust, portions of which occasionally coming within the sphere of the
earth’s attraction are drawn to its surface. Meteoric iron is too rare to
be of any value as a source of iron, but certain specimens have been
found in which the metal was malleable and of excellent quality. From
such meteorites the natives of India and other places have, it is said,
sometimes forged weapons of wonderful temper and keenness, and we may
well imagine that when such weapons have been made from iron that
had actually been observed to fall from the sky, they would be regarded
as endowed with magical powers, so that we may perhaps ascribe to such
circumstances the origin of some of the legends about enchanted swords,
etc. It is significant also that in some Egyptian inscriptions of the very
highest antiquity, the word indicating iron has for its literal meaning
stone of the sky.
But as nature has hardly provided man with the metal iron, he has
been obliged to find the art of extracting it from substances which are
utterly unlike the metal itself. In this case, as in many others, the art
has been discovered and practised ages before any scientific knowledge
of the nature of the processes employed had been acquired. The idea
prevails that there are such difficulties in extracting this metal; that
elaborate and complex appliances, not unlike those in use in modern
times, were requisite for the purpose; and therefore that the use of iron is
compatible only with a somewhat late period in man’s history, and
implies a comparatively advanced stage of civilization. Now there
undoubtedly are facts which tend to confirm this view; for instance, the
Spaniards who first colonized North America found the natives perfectly
familiar with the use of copper, but without any acquaintance with iron,
although the region abounded with the finest ferruginous minerals; and,
again, the archæologists who have examined the relics of ancient civilizations
and of pre-historic peoples about the shores of the Mediterranean,
find in the earliest of these relics weapons and implements of rudely
chipped stones, followed later by the use of better-shaped and polished
stones; hence the periods represented by these, they have respectively
designated by the terms palæolithic and neolithic—the old and the new
stone ages. At some later time the stone of these implements was
gradually replaced by bronze, which is a mixture of copper and tin, while
as yet iron does not occur in any form among the remains. In the latest
layers, however, articles of iron are found, and it is inferred that this
metal came into use only after bronze had been known for an indefinite
period; hence these later pre-historic periods have come to be respectively
called the bronze age and the iron age. No doubt this succession
really occurred in the localities where the observations were made, but it
would not be justifiable to assume that the same was the case in every
part of the world, for much would depend on such circumstances as the
presence or absence of the essential minerals. We may also set against
the supposed difficulty of obtaining iron from the ores, the still greater
complexity of the methods required for the production of copper and of
tin. Besides this is the fact that the ores of tin are found but in very few
places in the world, and of these only the Cornwall mines, so well known
33in ancient times, would be likely to furnish a supply to the places where
pre-historic bronzes are found; this implies that navigation and commerce
must have already made considerable progress. On the other
hand, iron has been produced and worked for untold ages by the negro
races all over Central Africa, and the method of treating the ore has no
doubt been that which is there still practised by certain scarcely civilized
tribes, and it is as simple as any metallurgical operation can possibly be,
requiring merely a hole dug in a clay bank, wherein the fuel and
minerals are piled up, and the mere wind supplies sufficient blast to urge
the fire to the needful temperature, or air is blown in from rude bellows
made of a pair of skins alternately raised and compressed. These very
primitive furnaces have in some places developed into permanent clay
structures, seven or eight feet in height. The natives of Central Africa
have therefore long known the method of extracting iron, as well as of
forging and casting it.
The nature and value of what has been done during the century in
the treatment of iron would not be intelligible without some description
of the ordinary processes of extracting the metal from the ores; and a
scientific understanding of these implies some acquaintance with
chemistry. Not because metallurgy has been developed from chemistry,
for the fact is rather the reverse; indeed, as we have seen, the art of
extracting iron from its ores was practised ages before chemistry as a
science was dreamt of. Although we may assume that many of our
readers have sufficient knowledge of chemistry to attach distinct ideas to
such few chemical terms as we shall have occasion to use, yet it may be
of advantage to others to have some preliminary notes of the character
of the chemical actions, and of some properties of the substances that
will have to be referred to. It is certainly the case that people in general,
and even people very well informed in other subjects, have but the
vaguest notions of the nature of chemical actions, and of the meaning of
the terms belonging to that science. For example, one of our most
popular and justly esteemed writers, treating of the very subject of iron
extraction, calls the ore a matrix, thereby implying that the iron as metal
is disseminated in detached fragments throughout the mass, which is a
conception inconsistent with the facts. The reader will be in a more
advantageous position for understanding the relation of the ores of iron
to the metal, if he will follow in imagination, or still better in reality, a
few observations and experiments like the following—of which, however,
he is recommended not to attempt the chemical part unless he is himself
practically familiar with the performance of chemical operations, or can
obtain the personal assistance of someone who is. Taking, say, a few
common iron nails, let him note some obvious properties they possess:
they have weight—are hard and tough so that they cannot be crushed in
a mortar—are opaque to light—if a smooth surface be produced on any
part, it will show that peculiar shiny appearance which is called metallic
lustre, in this case without any decided colour—they are not dissolved by
water as sugar or salt is—and are attracted by a magnet. If several of
the nails be heated to bright redness they may be hammered on an
anvil into one mass, and this may be flattened out into a thin plate, or it
may be shaped into a slender rod and then drawn out into wire; or
otherwise the nails may be converted into the small fragments called
iron filings. In these several forms the nails, as nails, will have ceased
to exist; but the material of which they were formed will remain
34unchanged, and each and every part of it however large or small will
continue to exhibit all the properties noted above as belonging to the
substance of the nails, which in the cases supposed has undergone
merely physical change of shape. Treating our nails in yet another way,
we may proceed to subject them to a chemical change, by an experiment
very simple in itself, but involving certain precautions, by neglect of
which the tyro in chemical operations would incur some personal risks;
these might however be obviated by using only very small quantities of
the materials (a mere pinch of iron filings and a few drops of sulphuric
acid), when the results would still be sufficiently observable. A few of
the iron nails having been placed in a flask of thin glass, we pour upon
them a mixture of oil of vitriol (sulphuric acid) and water, which has previously
been prepared by gradually adding 1 measure of the acid to 5
measures of water. The action that takes place is greatly accelerated by
heat, and indeed the contents should be heated to boiling by standing
the flask on a layer of fine sand spread on an iron plate and gently heated
from below. The nails will soon disappear, being completely dissolved
by the acid liquid, and the turbid solution should be filtered through
filtering paper as rapidly as possible and while still hot. This turbid and
dirty looking condition is due to foreign matters in the nails, for these
never consist of pure iron. The filtered liquid is set aside to cool in a
closed vessel, in which after a time will be found a deposit of crystals of
a pale bluish-green colour. The liquor above these having been poured
off, the crystals are to be rinsed with a very small quantity of cold water,
and then dried between folds of blotting-paper, after which they are
ready for examination. The quantity of the diluted acid put into the
flask should have a certain proportion to the weight of the nails; about 5
fluid ounces to 1 ounce of iron will be found convenient, for if less is used
the nails will not be entirely dissolved, and an excess will tend to keep the
crystals in solution instead of depositing them when cold. The nails—as
such—will now have passed out of existence: can we say that the iron
that formed them exists in the crystals? Certainly not as the metal iron,
for every property of the metal will have disappeared. The crystals are
brittle, can be crushed in a mortar—they are translucent—they show no
metallic lustre, but only glassy surfaces—they are readily dissolved by
water—they are not attracted by a magnet. The most powerful lens will
fail to show the least particle of iron in them; they have in their properties
no assignable relation to the metal of the nails, but are matter of
quite another sort; and be it noted that this entire otherness is the
special and characteristic sign of chemical change. So complete is the
transformation in the case we have been considering that it would never
have been said that iron was contained in these crystals, but rather that
the metal had for ever passed out of existence, but for one circumstance;
and that is, that by subjecting the crystals to certain processes of chemical
analysis we can again obtain from them the iron in metallic state. Nay
more, we should find the weight of metal so obtained to be exactly equal
to that of the pure iron dissolved from the original nails, supposing of
course that we operated upon the whole of the crystalline matter so produced.
The inference therefore is that although every property of the
iron appeared to be absent from the crystals, the iron entering in them
retained there its original weight, and the correct statement of the change
would be, that in the crystals the iron had lost all its original properties
SAVE ONE, namely, its weight, or gravitating force, if we choose to call it
35so, a property belonging to it in common with every material substance.
Chemical analysis can also separate from the crystals their other constituents
and weigh them apart—so much water and so much sulphuric
acid—and when to these weights that of the iron is added, the sum
exactly makes up the weight of the crystals.
A still simpler experiment, which may be performed by anyone with
the greatest ease, may serve as a further illustration of the profound
nature of the change in the properties of bodies brought about by
chemical combination, and it will also serve as the occasion of directing
attention to a remarkable circumstance that invariably characterizes such
changes, and one that should always be present in our minds when we
are considering them. A yard of flat magnesium wire can be bought for
a few pence, and after its metallic character has been observed in the
silvery lustre disclosed by scraping the dull white surface, a few inches is
to be held vertically by a pair of tongs, or by inserting one extremity in
a cleft at the end of a stick, then the lower part is brought into contact
with a candle or gas flame. The metal will instantly burn with a
dazzlingly brilliant light, and some white smoke (really fine white solid
particles) will float into the air; but if a plate be held under the burning
metal, some of the smoke will settle upon it, together with white fragments
that have preserved some shape of the metallic ribbon, but which a
touch will reduce into a fine white powder, identical with the well-known
domestic medicine called “calcined magnesia”—a substance totally
different from the metal magnesium. The reader will scarcely require to
be told that in this burning the metal is entering into combination with
the oxygen of the air—by which that invisible gas somehow becomes
fixed in these solid white particles, so entirely unlike itself. But this
experiment might be so arranged that the quantities of magnesium and
oxygen entering into the magnesia could be weighed. For this purpose
special appliances would be required in order to ensure complete combustion
of the metal, for in the experiment as just described some small
particles are liable to be shielded from the oxygen by a covering of
magnesia, and the arrangement would have to be such that the whole of
the white powder could be gathered up and weighed. In the absence of
such appliances, and of a delicate balance, together with the skill
requisite for their use, the reader must for the time be contented to take
our word for what would be the result. In every experiment the
magnesia would be found heavier than the metal burned in the proportion
of 5 to 3; in other words, magnesia always contains (so the phrase
runs) 3 parts of magnesium combined with 2 of oxygen: never more nor
less. A definite proportion between the weights of the constituent substances
characterizes every chemical combination, and when this is once
determined in a single sample of the compound, it is determined for every
portion of the same, wherever found or however produced. But each
compound has its own particular proportion, that is, the quantitative
relations are different for each. For example, the two constituents of
water, hydrogen and oxygen, are combined in the ratio of 1 to 8, etc.; and
oxygen combines with metals in a ratio different in each case. Then
occasionally the same ratio of constituents occurs in compounds of different
composition. The elementary student is apt to suppose that this is
because of the law which he finds stated, probably in almost the first page
of his text-book: “Every compound contains its elements in definite
and invariable proportions”; and even well-educated people entertain
36the idea of the fact being “governed by” or “obeying” the law just
quoted,—a misconception arising from the other use of the word “law,”
as signifying an enactment. The real case however is the converse;
namely, that a multitude of facts like that above stated have governed
the law, and caused it to be what it is—the general statement of many
observed facts.
We have assumed that the reader’s chemical knowledge had already
made him aware that in every case of ordinary combustion the oxygen
of the atmosphere is in the act of entering into combination with the
burning body: as with the magnesium, so with a coal fire, a gas flame,
or a burning candle; only in these last cases the products of the combustion
pass away invisibly. The candle by burning disappears from
sight, but its matter is not lost, and as in the case of magnesium, the compounds
it forms weigh more than the unburnt candle. The experiment
is commonly shown in courses of elementary lectures on chemistry, of so
burning a candle that the invisible products are retained in the apparatus,
instead of being dissipated in the atmosphere, and the increase of weight
of the burnt candle over the original one is demonstrated by the balance.
Important as is the part played by oxygen in all chemical actions on the
earth, the composition of the atmosphere was not understood until the
end of the eighteenth century, and it was well on into the nineteenth
before the quantities of its constituents were accurately determined.
Now everyone knows that air is mainly made up of a mixture of the
two gases oxygen and nitrogen. A mixture of two or more things is very
different from a chemical combination of them; for in the former each
ingredient retains its own properties. (See Air in Index.) Nitrogen
being an inert gas that takes no part in combustion, or in the ordinary
chemical actions of the air, acts therein simply as a diluent of the oxygen.
It is necessary in relation to our present subject to bear this in mind, as
well as the relative quantities of the two gases in air. For our immediate
purpose we may neglect the minor constituents of air—such as watery
vapour, carbonic acid, etc., of which the total weight does not exceed
one hundredth part of the whole—and consider air as a mixture of 23 parts
by weight of oxygen with 77 of nitrogen, or calculated in volumes, 21
measures of oxygen with 79 of nitrogen. Compounds of oxygen with
nearly every one of the other seventy or more chemical elements are
known, and these compounds, which are called oxides, are arranged by
chemists under five or six classes, forming as they do basic radicles, acid
radicles, saline oxides, etc. With some of these compounds belonging to
different classes, we must make acquaintance after noticing the elementary
substance with which the oxygen is united.
We begin with carbon, which forms the chief constituent of all our combustibles.
Some specimens of graphite, plumbago, or “blacklead” consist
of almost pure carbon (98 per cent.), and some varieties of wood charcoal
exceptionally contain 96 per cent.; but in ordinary charcoal the percentage
is much less. Coal, the most familiar of our solid fuels, varies greatly
in composition, carbon being the predominating constituent, in amount
from 57 to 93 per cent. Coke, another fuel much used in metallurgical
operations, is made by heating coal without access of air, when a large
quantity of gaseous substances is expelled. Coke burns with an intense
and steady heat without emitting any visible smoke, but it does not ignite
as readily as coal. Carbon forms two different compounds with oxygen:
both are invisible gases, but they differ in the proportions of the constituents,
37and present different properties. When carbon (coal, coke, or
charcoal) is completely burnt, that is, with an abundant supply of air, the
product is carbonic acid gas, in which 3 parts of carbon are combined
with 8 of oxygen: when, on the other hand, the carbon is burnt with a
sufficiently restricted access of air, the result is carbonic oxide gas, in
which 3 parts of carbon are united with only 4 of oxygen. The reader
will here observe that the former contains just twice as much oxygen as
the latter for the same quantity of carbon. This fact and numberless
others like it are expressed or summed up by another law of chemical combination
which states that when two elements combine in several different
proportions these are invariably such that the ratios in the several compounds
will be found to have exact and simple numerical relations; that
is, such as may, when reduced to their lowest terms, be expressed by the
simple integers 1, 2, 3, etc., as 1 : 2, 3 : 2; ... 8 : 9, etc. It comes to the
same thing if we compare together the weights A and A´ which are
united in each compound with any one identical weight of B, giving of
course the ratio A : B ÷ A´ : B. For instance, in the case just given, of
carbon and oxygen, 3 : 4 ÷ 3 : 8 = 2 : 1. This, which is simply stating
the facts, is called the law of multiple proportions. On a later page will
be found another illustration (see Index, Nitrogen and Oxygen Compounds),
and its expression in terms of the atomic theory, which goes
behind the facts (so to speak), but is extremely useful by comprehending
many other groups of facts in chemistry and in other sciences. Carbonic
acid gas is of course incombustible, but carbonic oxide gas burns by
uniting with the additional proportion of oxygen and becoming carbonic
acid. On the other hand, carbonic acid gas passing over red-hot coals
takes up from them the additional proportion of carbon, and is, we may
say, unburnt into carbonic oxide. When we see a pale blue flame flickering
over the bright embers in a fire grate, it is carbonic oxide burning
back again by taking more oxygen from the air above the coals. Carbonic
oxide combines directly with two or three of the metals, as, for
instance, it forms a volatile compound with nickel, at a certain temperature,
and this is decomposed again at a higher temperature. The like
takes place with iron, although in very small quantities, but the observation
throws some light on the processes of reduction. Carbonic oxide is
neither acid nor basic, but carbonic acid is an acid oxide, and as such unites
with oxides of the basic class to form another range of compounds. Thus,
for example, the oxide of the metal calcium is quicklime, which is strongly
basic, and this directly combines with carbonic acid, forming a neutral
substance called in systematic chemistry calcium carbonate, or more
commonly but less correctly, carbonate of lime, familiar to everyone in
the compact state as limestone, and marble, and in a more or less pulverent
condition as chalk. When any of these is heated to redness,
carbonic acid is expelled and quicklime remains. Like most oxides,
quicklime forms a compound with water, the combination being attended
with the extrication of much heat, the compact quicklime swelling and
crumbling into slaked lime. The chemist’s term for a compound of a
basic oxide with water is hydrate, while that of an acid oxide with water
is for him properly an acid, or in order to particularly distinguish this
class, an oxy-acid. It was however the older practice to give the name
of acid to the oxide alone, and this naming having found its way into
popular language is much more familiar to the non-scientific reader.
The systematic names of the two compounds of carbon and oxygen are
38carbon monoxide and carbon dioxide, but we shall use here the more
familiar terms carbonic oxide and carbonic acid.
We have now to call attention to a substance which contributes by far
the largest part to the solid crust of our globe. It is called silica, from
silic-, the Latin word for flint (without case suffix): it is seen in flint, and
very pure in rock crystal, quartz, agate, and calcedony. It forms the
essential part of every kind of sand and sandstone, and is the principal
ingredient of clay, granite, slate, basalt, and many other minerals.
Silica is the oxide of a quasi-metal called silicon, which can be obtained
from silica with difficulty, and only by roundabout processes, presenting
itself in different conditions according to the process used. Silica is an
acid oxide, and it readily unites with most of the basic oxides when
heated with them, forming a class of compounds of different properties
which are much modified in admixtures containing two or more. Very
few of these silicates are soluble in water, most of them are not: they
are all fusible at various temperatures, except silicate of alumina, of which
fire-clay is chiefly constituted. Alumina, it should be stated, is the oxide
of the metal aluminium. The silicates of lime and of magnesia fuse only
with great difficulty; but the silicates of iron and of manganese are easily
fused, and silicate of lead still more so. Glass is a mixture of silicates,
often of lime, soda, and alumina; sometimes of lead and potash mainly;
porcelain and pottery consist chiefly of silicate of alumina with varying
proportions of silicates of iron, of lime, etc.
It now remains only to mention two non-metallic elements that are
nearly always present in crude iron, but which the metallurgist strives
to eliminate, as they are in general very injurious to the quality of the
material even when their amount is very small. The first is sulphur, well
known as brimstone, also as flowers of sulphur, a yellow coloured solid,
which burns in the air. The product of the combustion is an invisible
gas of a readily recognized pungent odour: this is an acid-forming oxide
containing equal weights of sulphur and oxygen. There is another oxide
in which the weight of oxygen is one and a half times that of the sulphur,
and this is the radicle of the very active sulphuric acid or oil of vitriol.
Sulphur, like oxygen, unites with most of the other elements, forming
compounds called sulphides. Of these the iron compound called pyrites
is the best known, and its occurrence in coal prevents the use of that
material as fuel in contact with iron or other metals. Phosphorus is an
element that occurs naturally only in combination; in its separated state
it is a very inflammable solid. It combines directly with other substances
and is taken up by some fused metals in large quantities. In many
cases a very small proportion of it existing in a metal greatly modifies
the properties of that metal. Phosphorus forms several oxides, and these
are radicles of powerful acids, among which is phosphoric acid that combines
with basic oxides to form phosphates.
We have now, in the few last paragraphs, set before the reader the
minimum of chemical knowledge that will enable him to follow the rationale
of such processes of the modern treatment of iron and its ores as we can
here give an outline of. Although there are numberless minerals from
which some iron can be extracted, the name of iron ore is confined to
such as contain a sufficient amount to make the extraction commercially
profitable, and this requires that the mineral should be capable of yielding
at least one-fifth of its weight. The ores are very abundant in many
parts of the world, and they consist mainly of oxides and their hydrates,
39or of carbonate, or of carbonate mixed with clay and silicates, sometimes
also with coaly matters in addition. The carbonate iron ores are often
mixed with oxides. Each class of ore is liable to be contaminated with
phosphates and with sulphur. The richest ore is the magnetic iron ore,
which is found in enormous masses in Sweden, Russia, and North
America. It is an oxide containing 72·41 per cent. of iron. Red hæmatite
and specular ore are varieties of another oxide with 70 per cent. of iron:
the former is a very pure ore when compact. It is found in Lancashire,
Cumberland, and South Wales, and much has been imported from Spain,
while America has abundant supplies near Lake Superior. Specular iron
ore forms brilliant steel-like crystals which show the red colour of hæmatite
only when scratched or powdered. Elba was famous for this ore, which
occurs also in Russia and Sweden, and large deposits are met with
in both North and South America. Brown hæmatite is a hydrate of
the former, containing 60 per cent. of iron; it abounds in France
and Spain, where some kinds are associated with a noteworthy quantity
of phosphate of iron. Spathic or sparry iron ore is, when pure, a
collection of nearly colourless transparent crystals, consisting of carbonate
of iron; it contains about 48 per cent. of iron, and also some
of the metal manganese, which last circumstance makes it, as we shall
see, particularly suitable for producing certain kinds of steel—indeed
it is sometimes called steel ore. Large beds of it occur in Styria and
Carinthia. Clay iron stone, or clay-band, has been extensively mined in
Britain. It is found abundantly in Staffordshire, Yorkshire, Derbyshire,
and South Wales. It consists of carbonate of iron intimately mixed with
clay. The quantity of iron in some samples falls as low as 17 per cent.,
but it rises with variations to as much as 50 per cent. Much of its importance
arises from the fact of its occurring in beds alternating with layers
of coal, limestone, and clay, so that the same pit is sometimes able to
supply firebricks for building the furnace, fuel for the smelting, and limestone
for the flux,—a combination of advantages that for long enabled iron
to be produced in England cheaper than elsewhere. The like is true of
the blackband ore, which, in addition to the same ferruginous composition
as the last, contains also so much combustible or bituminous material
that it can be calcined (roasted) without additional fuel. The deposits of
blackband in Lanarkshire and Ayrshire, which were discovered only in
1801, have given great industrial importance to the district. Yet another
British ore must be noticed, namely, the Cleveland ironstone of the
North Riding of Yorkshire. This is a carbonate of a grey or bluish
colour caused by the presence of a little iron silicate. It contains also a
considerable amount of phosphorus.
How simple is the operation of obtaining iron from the ore has already
been stated—that it is necessary only to surround lumps of ore by fuel
in a fire urged by a natural or artificial blast, and then to hammer the
mass extracted from the furnace so as to weld together the scattered
particles of the metal, and at the same time squeeze out the associated
slag and cinders, in order to obtain a coherent malleable piece, which
can be reheated in a smith’s fire, and forged into any required form. It
is no wonder therefore that iron was so produced by the ancient Britons;
at any rate Cæsar found them well provided with iron implements and
weapons. No doubt the Romans brought their more advanced skill to
the working of the metal; but in the matter of treating the original ore,
the methods they pursued on an extensive scale in Britain were of the
40rude kind already described. Indeed in localities where the Romans
were known to have carried on their operations, the remains of their
workings are almost always found on high ground, so that it may be
inferred that they relied upon the winds to fan their fires, and their operations
were incomplete and wasteful. The most extensive of them appear
to have been in Sussex and Monmouthshire, in which last county there
are places where the ground is in large areas covered by their cinders and
refuse, and in this about 30 or 40 per cent. of iron occurs, so that for some
centuries this material was found capable of being profitably reworked as
a source of the metal. Iron continued to be produced in England during
the middle ages with charcoal for fuel, but its export was forbidden, and
whatever steel was required had to be imported from abroad. Afterwards
German artisans were brought over for making steel, and soon afterwards
the importation of shears, knives, locks, and other articles was prohibited.
The native production of iron continued, and this consumed the forests
so rapidly for the supply of charcoal, that various Acts were passed to
restrain the iron-makers, in order to preserve the timber. In spite of
these, the arts of smelting and working iron advanced apace: bellows
were used for the blast, and then the works were brought down into
the valleys, where water power could be employed to work them. The
scarcity of charcoal fuel caused many attempts to supply its place with
pit coal, but these met with small success, partly on account of the coal
containing so much sulphur, and partly from the difficulty of obtaining
with it a sufficiently high temperature, especially as the blowing apparatus
was as yet very imperfect. At length, in the first half of the seventeenth
century, the problem was solved by Dud Dudley, whose process was kept
secret, but is believed to have consisted in supplying coal at the top of a
higher furnace, in such a manner that the coal was converted into coke
by the heat of the escaping gases before it reached the reducing zone of
the furnace. This innovation was violently opposed by the charcoal
smelters, who persecuted the inventor in every way, until their resistance
was successful. But before the middle of the next century coke was
regularly used in iron smelting, the process having been made successful
by Darby at Coalbrookdale, and then many new applications of cast iron
came into vogue. Coke being a substance burning less freely than charcoal,
bellows were found inadequate to give the necessary blast, and were
displaced by blowing cylinders, actuated at first by water wheels, but this
uncertain and comparatively feeble source of power was soon superseded
by the steam engine, the “fire engine,” for which, as we have seen, Watt
obtained his patent in 1769. The furnaces were not then all engaged in
producing the fusible metal now called cast or pig iron as are the huge
blast furnaces we see at the present time. Indeed it was much to the
disgust of the old iron smelter that occasionally his product turned out
to be of the fusible kind, unworkable by the hammer, which therefore he
regarded as worthless. At what date cast iron was first used is uncertain;
but probably it was not long before the fourteenth century. The furnaces
in use up to that time were small square walled-in structures only 3 or 4
feet high, and their effect would not greatly exceed that of a smith’s forge:
but as improved blowing apparatus gave more power, they soon became
enlarged into oval or round brick towers from 10 to 15 feet high, and they,
like the small furnaces, could be made to yield either smith iron or steel
by modifying the charge and the manner of applying the blast; while
furnaces of dimensions exceeding a certain limit could no longer be trusted
41to turn out malleable metal, but they produced instead the cruder substance
we call white pig iron, and this requires much subsequent treatment
before it is converted into malleable or “merchant iron.” Nevertheless
the demand for cast iron as such, and more particularly the
adoption of improved methods of deriving malleable iron from it, caused
further increase in the size and numbers of blast furnaces, until in the
early part of our century 30 feet was not an unusual height, the highest
one in England in 1830 attaining 40 feet. The total make of pig iron in
England was in that year nearly 700,000 tons, perhaps about fifty times
as much as it was a century before, and thirty years later (1860) it had
risen to nearly 4,000,000 tons. These figures show the extraordinary
expansion of the British iron manufacture in the earlier part of the century;
and the still more extensive applications of iron during the next twenty
years had the effect of almost doubling the produce in 1880, and of
42increasing also three-fold the amount of foreign metal imported, raising it
to 2,500,000 tons. The reader will now, it is hoped, be prepared to follow
with some interest a brief account of the principal inventions which have
brought about results of such importance.
Fig. 17.—Blast Furnace (Obsolete Type).
Fig. 18.—Section and Plan of Blast Furnace (Obsolete Type).
Deferring for the moment any description of the latest blast furnaces,
we invite his attention to Fig. 17, which represents the furnace used in
the first half of our century, but which now is of an obsolete type, Fig. 18
being the section and plan of the same. The lower part of Fig. 17 shows
43where the molten metal has been allowed to run out of the furnace into
channels made in dry sand; first a main stream, then branches to right
and left, each of these with smaller offsets on each side of it. These
smaller channels are the moulds for the pigs, so called because of the
fancied resemblance of their position with regard to the branch that supplied
them, to the litter of a sow. They are easily broken off from the larger
mass, and then form pieces about 3 ft. long with a ᗜ-shaped section,
4 in. wide, the weight being from 60 to 80 lbs. This is iron of the crudest
kind, and though it is often referred to as “cast iron,” it is, as a matter
of fact, not used in this state for any castings, except those of the very
roughest and largest kind: a certain amount of purification is requisite in
most cases. This is given by fusing the metal—along with some form of
oxide and often other matters—in a cupola furnace, which is like a small
blast furnace, being from 8 ft. to 20 ft. high and uses coke for fuel with a
cold blast.
So far from being simply iron, pig contains a large and variable proportion
of other matters amounting often to 10 or 12 per cent.; and these
confer upon it its fusibility. The principal one is carbon, which is found
in the metal partly in the state of chemical combination with it, and
partly in the form of small crystals similar to those of graphite or
plumbago, disseminated through the mass. When there is a comparatively
small proportion of the carbon combined with the iron, the substance
is grey, and it can be filed or drilled or turned in a lathe. In
white cast iron the combined carbon predominates, or is sometimes
accompanied by scarcely any graphitic carbon; it is brittle and so very
hard that a file makes no impression. It fuses at a lower temperature
than the other varieties. A third kind is the mottled cast iron, which
shows a large coarse grain when broken, and distinct points of separate
graphite particles; it is tougher than the others, and therefore when
cannon were made of cast iron this variety was preferred. The following
table giving the percentage composition of four samples of crude cast
iron will show their diversities.
White.
White.
Mottled.
Grey.
Iron
88·81
89·304
93·29
90·376
Combined carbon
4·94
2·457
2·78
1·021
Graphite, or uncombined carbon
...
0·871
1·99
2·641
Silicon
0·75
1·124
0·71
3·061
Sulphur
trace
2·516
trace
1·139
Phosphorus
0·12
0·913
1·23
0·928
Manganese
5·38
2·815
trace
0·834
The reader will observe that the last item in the table above is a substance
that he has not yet made the acquaintance of, namely, manganese.
This is a metal which in many of its chemical relations much resembles
iron, and ferruginous ores usually contain a greater or less proportion of
it. Manganese is of great importance in the manufacture of steel, as we
shall presently see; but as a separate metal it has no application, and is
obtainable in the metallic state with much difficulty. One of its oxides
has however very extensive applications in the chemical arts, and others
44form acid radicles, which in combination with potash or soda give rise to
useful products. The well-known “Condy’s fluid” is a solution of one of
these.
We have seen how malleable iron or steely iron may be directly
obtained from the ores, but it has been found that on the large scale it is
necessary and more economical to operate on the pig iron produced by
the blast furnaces in such a manner as to remove the greater part of the
foreign substances.
Fig. 19.—Section of a Reverberatory Furnace.
The first step in the conversion of the pig iron usually taken has been,
and to a certain extent even is still, to remelt the metal in what is termed
a finery furnace, a kind of forge in which a charcoal fire is urged by a
cold blast, and so regulated that an excess of oxygen is supplied, or rather
more than would suffice to convert all the carbon of the fuel into carbonic
acid; although this is perhaps not absolutely necessary, as carbonic acid
would itself supply oxygen by suffering reduction to carbonic oxide. At
any rate the melted metal is exposed to an oxidizing atmosphere and
constantly stirred. Many different arrangements of the furnace and
details of the process have been used. For instance, where the finest
quality of malleable iron was not aimed at, coke has been the fuel
employed, and many shapes of furnaces, etc., have been contrived, and
various additions of ores, oxides, etc., made to the charge, according to
local practice and the nature of the crude iron. One marked effect of the
operation is the final removal of nearly all the silicon, which is burnt or
oxidized into silica, and this at once unites with oxide of iron, which is
also formed, to produce a readily fusible slag of silicate of iron, and in the
production of this silicate any sand attached to the pig will also take
part. Much of the carbon, amounting sometimes to more than half, is
also eliminated as carbonic oxide, and of what is left but little remains in
the graphitic state. The action on the phosphorus is usually less marked,
but there is always a notable reduction of the quantity. The sulphur is
also lessened in some degree, although when coke is used, the fuel has
the disadvantage of itself containing sulphur, phosphates, and other
deleterious matters. Sometimes a little lime is added to the charge to
take up the sulphur from the coke. The operation lasts some hours, the
fused metal being frequently stirred with an iron rod, until it assumes a
pasty granular condition, when the workman gradually collects it upon
the end of the rod into a ball of about three-quarters of a cwt. in weight.
These balls, or blooms as they are called, are removed from the furnace
while still intensely hot, and at once submitted to powerful pressure by
means of some suitable mechanical arrangement, the effect being to
squeeze out the liquid slag and force the particles of metal together by
which the whole becomes partially welded into a more compact mass.
Then this mass is, while still hot, either hammered with gradually
increased force of the strokes, or in the more modern practice, passed
between iron rollers (these we shall presently describe), by which it is
shaped into a bar. The bars are afterwards cut into lengths, reheated
without contact of fuel, again hammered or re-rolled; and this process is
several times repeated when the best product is required. During the
first treatment of the blooms, and also in the subsequent hammering or
rolling, the oxygen of the atmosphere acts on the surface of the glowing
metal, so as to cover it with thin scales of oxide, and these, carried into
the interior of the mass, will give up their oxygen to any residual silicon,
carbon, etc., producing a little more slag, carbonic oxide, phosphate of
45iron, etc., which by the pressure of the hammers or rolls are ultimately
forced out of the metal. It will be observed that in producing the pig
iron the chemical action is the separation of oxygen from the metal,
while conversely an oxidizing action is set up in the finery and subsequent
treatment, in order to burn off the foreign ingredients. But this cannot
be done without at the same time re-oxidizing some of the iron itself, of
which therefore there is always a considerable loss, by its formation into
slag (silicate), cinder, foundry scale (oxide), etc. The quantity of iron
lost depends of course on many conditions, such as the care exercised in
the operations, but it occurs in all the processes that have been devised
for the conversion in question, even in the most modern: its amount
may be taken to range between 10 and 20 per cent. The reader is
requested to bear in mind the nature of the chemical actions that have
just been described, for in even the most recently invented processes the
principle is the same in nature and effect. So completely can the foreign
elements be eliminated by this, or some analogous process, such as we
shall presently mention, that the finest Swedish bar iron contains more
than 99½ per cent. of the metal, and in some cases only a very little carbon
and a mere trace of phosphorus remain, amounting together to less than
1 part in 2000. Such metal is made from very pure ore, containing no
sulphur and scarcely any phosphorus, while charcoal is the fuel used
in all the operations. As already mentioned, the objection to the use
of coke is the sulphur, phosphates, and siliceous matters it contains.
Toward the close of the eighteenth century an invention came into use
which obviated the disadvantages of the cheaper fuel for converting
crude iron. This was the puddling furnace, brought into use after much
experimenting by Henry Cort in 1784. In it the pig iron is fused in a
reverberatory furnace, the form of which will be understood from Fig. 19,
which is a diagram showing such a furnace in section, where f is the fire,
a an aperture at which the fuel is introduced, p the ash pit, b is a low
46wall of refractory material called the “bridge,” over which the flame
passes, and is by the low arched roof reflected or reverberated downwards
upon the charge, c, which is laid on a hearth, or iron floor, having spaces
below it where air circulates in order to prevent it becoming too hot.
In Cort’s original arrangement the bed of the hearth was formed of sand,
which gave rise to much inconvenience by producing a quantity of the
very fusible silicate of iron, that speedily attacked the masonry of the
furnace, and therefore a very important improvement was devised some
years later by S. B. Rogers, who made the bed of his furnace of a layer of
oxide of iron, spread on a cast iron plate 1½ inches thick. In later times
it has become usual to cover the iron hearth with certain other refractory
mixtures varied according to circumstances, of oxide, ore, cinder, lime,
etc. There is one of these mixtures significantly designated “bull-dog”
by the workmen. We may mention here that it has, in more recent
times, when very high temperatures are obtainable, been found unnecessary
to cause even the flame to come into contact with the substances
on the hearth, inasmuch as the heat radiated from the flame and the
intensely heated roof of the furnace suffices, so that in consequence of this
the roofs are now constructed nearly flat. In the puddling furnace the
melted metal is constantly stirred, and no little skill is required to
regulate the fire by the damper on the chimney, and to admit the proper
amount of air to mix with the flame. The pig iron softens and melts
gradually, until at length it becomes perfectly liquid, at which stage it
swells up and appears to boil owing to the escape of carbonic oxide in
numerous jets, which burn with the characteristic pale blue flame. The
puddler then briskly stirs the mass to cause more complete oxidation of
the carbon, silicon, etc., by bringing the superficially formed oxide of iron
into the interior. As the iron loses its carbon, it assumes much the
texture of porridge, consisting of pasty lumps of malleable iron implexed
with the liquid slag (silicate of iron, etc.) which drips from the spongy
balls as the puddler collects them at the end of his stirring rod, as in the
finery operation. The next thing is to run the mass immediately between
powerful rolls (puddling rolls) by which the slag is squeezed out, as
before, and finally through the finishing rolls that shape it into bars or
plates.
When a comparatively impure pig iron is used or when a better quality
of malleable metal is desired, the crude iron is submitted to a preliminary
treatment before puddling. This treatment, by a technical distinction,
called refinery, is practically identical with the finery process already
described, except that instead of being collected into blooms, the fluid
metal is run out to form a layer 2 or 3 inches thick, and this, before
becoming quite solid, is suddenly cooled by having water thrown over it,
the result being a white, hard, brittle mass, which broken into pieces is
ready for the puddling furnace.
The operation that has been described is known as hand puddling, in
contradistinction to later methods in which it has been sought to substitute
some form of machine that will produce the same result automatically,
such as revolving furnaces, etc. It has been found difficult to
maintain these in good working order, and in England at least mechanical
puddling has never found much favour, but in the great iron works of
Creusot, in France, large revolving furnaces were in use about 1880, which
could turn out 20 tons of converted iron in 24 hours, whereas the old
hand puddling furnaces could in the same period produce only 2½ or 3
47tons, with two sets of men, the puddler and one assistant. Of these
mechanical furnaces it is unnecessary to give any account, especially as
the puddling process itself has nearly gone out of use, having been superseded
by more economical methods.
The use of rolls for treating the product of the puddling furnace, and
for making it into bars, was also an invention of Henry Cort’s, for which
he obtained a patent in 1783. This was in many respects an immense
improvement on the older system of hammering; it is still practised, and
by it shapes can be given to the metal scarcely possible on the older
system, while the tenacity of the metal is increased by the uniformity
given to the grain. The difference of chemical composition between cast
and wrought iron the reader has already been made acquainted with, and
there is quite as great a difference in their textures. The former, when
broken across, shows a distinctly crystalline structure, which we may
compare to that of loaf-sugar, while the latter exhibits grain, not unlike
that of a piece of wood. This fibrous structure depends upon the mechanical
treatment of the iron, and in rolled bars the fibres always arrange
themselves parallel to the length of the bar. Fig. 20 shows this fibrous
structure in a piece of iron where a portion has been wrenched off. Like
wood, wrought iron has much greater tenacity along the fibres than across
them; that is, a much less force is required to tear the fibres asunder
than to break them transversely. Consequently, to obtain the greatest
advantage from the strength of wrought iron, the metal must be so
applied that the chief force may act upon it in the direction of the fibres.
Near the beginning of our article on Iron Bridges (q.v.) the reader will
find some illustrations of the very different resisting powers of cast and
wrought iron.
Fig. 20.—Fibrous Fracture of Wrought Iron.
Nothing in the way of inventions can be compared to those of Cort’s as
to the effect they have had in promoting the iron industry, until we reach
a period some years after the middle of our century; but we must not
neglect to recognize the scarcely inferior importance of Rogers’ improvement.
48Singularly enough, neither of these men reaped any benefit from
his inventions. Cort died in the last year of the eighteenth century, quite
a poor man, having been supported only by a niggardly pension of some
£160 from the Government, and leaving his family in indigent circumstances.
Yet a most eminent authority on iron questions (Sir W. Fairbairn)
estimated—some time about the middle of our era—that the two
inventions of Cort’s alone, the rolling-mill and the reverberatory puddling
furnace, had by that time added to the wealth of Great Britain by an
amount equivalent to six hundred million pounds sterling. For many
iron-masters had profited by these inventions, amassing very great
fortunes, in some instances also acquiring titles of honour. Clearly to
Cort and Rogers may be applied the sic vos non vobis saying.
We shall now turn to the improvements that have been effected in the
blast furnace, and of these none perhaps has been more marked than
that made by Neilson, when in 1828 he substituted heated air for the
ordinary cold air that had before always supplied the blast. It will be
remembered that the heat is due to the combination of only the oxygen
of the air with the carbon of the coke, but the greater part of the air—the
four-fifths of nitrogen—take no part in the action, beyond abstracting
a large proportion of the heat; but when the air is heated to a high temperature
before entering the furnace, the cooling effect of the nitrogen is
greatly obviated, and consequently a much higher temperature is obtained
at the place of combustion, and the requisite intensity of heat is at once
produced, which is most effective in completing the fusion and separation
from each other of the slags and iron, and also in accomplishing the
reduction of the oxide. But Neilson found that the net result of burning
some fuel to heat the air before entering the furnace was a great economy
of the total fuel required for smelting the ore. He had to encounter many
difficulties in carrying his invention into practice; the iron ovens first
used for heating the air were rapidly oxidized; and when thick cast iron
pipes were substituted, these were liable to leak at the joints on account
of the expansions and contractions caused by changes of temperature.
Then the new invention had as usual to contend with established prejudices
and misconceptions; but it soon came into use in Scotland, where
it effected a great saving; inasmuch as it was found possible to use with
the hot blast raw coal of a certain kind, plentiful in Scotland, because the
heat retained by the ascending gases sufficed to convert the coal at the
top of the charge into coke.
It will be remembered that the active agent in the reduction of the ore
is the carbonic oxide gas formed by the incomplete combustion of the
carbon of the fuel; or what comes to the same thing, the absorption by
carbonic acid first produced of another proportion of carbon. The
carbon oxide robs the iron oxide of its oxygen to become itself changed
into carbonic acid. In reality however the action is more complex than
this in its chemical relations; for instance, metallic iron will under
certain circumstances act conversely on carbonic acid, and rob it of half its
oxygen. The net result of the reactions between carbon, iron, iron oxide,
and these gases depends mainly upon the temperature and pressure and
upon the relative quantities of each substance present. In the gases
escaping from the blast furnace there is always a large quantity (nearly
one-third) of carbonic oxide. At the blast furnaces in work during the
first half of our century the combustible gases were allowed to burn to
waste as they issued from the top of the furnace, in the manner shown in
49Fig. 17, and at night the flames used to form a weird and striking feature
in the prospect of an iron-smelting region.
Instead of allowing the escaping gases to burn to waste, it became the
practice about 1860, and so continues, to draw them off and burn them under
steam boilers or use their flames for heating the blast. An effective method
of withdrawing the gases is shown in Fig. 21, which is a section through the
upper part of a smelting furnace, with the “cup and cone” arrangement.
The mouth of the furnace is covered by a shallow iron cone a, open
at the bottom, into which fits another cone b, attached to a chain c,
sustained by an arm of the lever d, which is firmly held in position by
the chain e, and is also provided with a counterpoise f. When the mouth
of the furnace is thus closed, the gases find an exit by the opening g,
seen behind the cones, and leading into a downward passage, through
which they are drawn by the draught of a tall chimney to the place where
they are burnt. The charge for the furnace is filled into the hopper a,
and at the proper time the chain, e, is slackened when the weight of the
material resting on the suspended cone overcomes that of the counterpoise,
and the charge slides down over the surface of the cone b, which is
immediately drawn up again by the counterpoise, so that the opening
into the air is at once closed.
Fig. 21.—Cup and Cone.
The march of improvement in the blast furnace has been characterized
particularly in Britain and the United States by a great increase of
dimensions, which is found to promote economy in fuel, etc. In the
former country the furnace of the latter part of our century is commonly
from 70 to 80 feet high, and some have even been built with a height of
more than 100 feet, while in the States the tendency to build very high
furnaces is still more marked. A single large furnace may turn out as
much as 1,500 tons of pig iron in a week, and some in America, it is said,
actually produce as much as 2,500 tons. The more usual output of a
blast furnace is however much less than these amounts; but if we say
only one-half, or even one-third of these quantities, a state of things
is indicated very different from what obtained about 1837, when the best
Welsh furnaces produced only 200 tons a week. If we go back to the
beginning of the century, the difference is much more marked, for the
50blast furnaces of that period could turn out only about 30 tons in a
week.
The proportions of fuel, ore, and limestone charged into the furnace
vary greatly according to the composition of the ore, the quality of iron
aimed at, and the practice of each manufacturer. It is usual previously
to calcine the carbonate ores and others also, in order to expel the
carbonic acid and the moisture, of which last all contain a considerable
amount: and sometimes the limestone is mixed with the ore to undergo
this preliminary process. The charge being conveyed from the roasting
kilns to the blast furnace while still hot effects an obvious economy of
fuel in the latter. In the case of hæmatite ore the quantities of materials
in one charge may be something like 54 cwt. of ore, 9 cwt. of limestone,
and 33 cwt. of coke. It is quite common to use mixtures of different
kinds of ore, so as to modify the quality of the product according to
particular requirements. The use of the limestone is to take up silica,
and the slag is found to consist mainly of silicates of lime and alumina.
The amount flowing from a blast furnace of course varies much according
to the conditions, and is larger than would commonly be supposed; for
the production of one ton of pig iron involves the production of from
½ to 1½ tons of slag.
Fig. 22 represents in section the later type of blast furnace, which of
course is circular in plan. Its height may be taken as 80 feet, and the
diameter at the widest part of the interior as 22½ feet, narrowed to 20
feet near the top. The lowest portion, C, is called the crucible, the
bottom of which is the hearth, both formed of the most refractory
materials obtainable. The conical widening, B, above the crucible is the
boshes, and at the top is seen the “cup and cone” apparatus already
described, A, surmounted by the short cylindrical iron mouth, through
apertures in which the charges are tipped from the gallery, D, these
having been raised there in small trucks by hydraulic or other elevators.
The escaping gases leave the furnace by the exit, E, which leads into the
“down-come,” G, and they are conducted from it to the “regenerative
stoves” and dealt with as presently to be described. Our section
represents the masonry of the furnace as sustained by pillars, P, at the
outside of the lower part; these pillars support a strong ring of iron
plates upon which the wall rests. This arrangement has the advantage
of allowing the workmen the greatest freedom of access to parts about
the crucible, which require much attention. Here, at the lowest part, is
an aperture from which the liquid iron is allowed to run out every five or six
hours, it being plugged in the meantime by clay and sand. The slag
being much lighter than the iron, floats above it, and runs off at a higher
level over the tympstone. Opening into the hearth are several orifices to
admit the hot blast from the nozzles of the tuyères, which of course do not
project into the furnace itself; but they are so near to the region of
intensest heat that they would be rapidly destroyed unless they were
surrounded by a casing through which a current of water is constantly
running. The tuyères, of which there may be 3 or 5, are supplied from
the pipe seen at K. The earlier plans of heating the air did not permit
of a very high temperature being given to the hot blast, about 600° F.
being the limit; but the “regenerative” stoves can supply a blast of
more than 1,600° F., or not far below the melting point of silver.
Another great increase has been in the pressure of the blast; 2 or
3 lbs. per square inch sufficed in the earlier practice; but the lofty
51modern furnaces have to be supplied with the blast at a pressure of
10 lbs. per square inch, and over. Even when comparatively low
pressures were the rule, a large ironworks required much blowing power.
The works formerly at Dowlais, in South Wales, for instance, had an
engine of 650 horse-power for the blowing engine, in which a piston of
12 feet diameter moved in a cylinder 12 feet in length. The quantity of
air that passes into a blast furnace amounts to thousands of tons per
week, its weight being much greater than that of all the ore, coke, and
limestone put together.
Fig. 22.—Section of Blast Furnace.
It need scarcely be said that great care and expense are bestowed on
the construction of these furnaces. Only the best and most refractory
materials, such as firebricks, are used for the lining, and the exterior is a
casing of solid masonry, strengthened with iron bands. When a new
furnace is finished it takes a month or six weeks to put it into operation;
but when this is done it will remain in action night and day continuously
52for a long period—perhaps for eight or ten years—before the necessity
for repairs requires a “blow out.” And the blow out and restarting,
without the cost of repairs, entail an outlay of several hundred pounds.
The gases leaving the throat of the furnace consist mainly of nitrogen
and a little carbonic acid, together with about one-third of their volume
of the combustible gases, carbonic oxide, and some hydrogen; but these
last do not leave the furnace in an ignited state, because the oxygen
there has already been consumed. They are conducted by the “down-come”
pipe, G, Fig. 22, to a point at which, by means of a valve, they can
be directed to one or other of two circular towers entirely filled with firebricks,
arranged chequerwise, so as to form innumerable passages
between them. The furnace gases are admitted at the bottom of the
Cowper tower, or “regenerative stove,” into a flue to which a regulated
quantity of air has access, and there they are fired: the flame ascending
the flue to the upper part of the tower, thence descends, communicating
its heat to the firebricks, which soon acquire a very high temperature,
especially where the flame first enters, and the burnt gases leave the
tower for a tall chimney, leaving most of their heat in the firebricks.
When this action has continued for a sufficient time, the connection of
the regenerator with the throat of the furnace is cut off, and the escaping
gases are directed into the other regenerator, and at the same time the
blast from the blowing engine is made to ascend among the firebricks
of the first, where gaining increasing temperature as it ascends—the
stove being hottest at the top—the air leaves the tower to be conducted
to the tuyères at such high temperature as already mentioned. While
the one regenerator is thus heating the blast, the other is in its turn
accumulating heat from the flames of the escaping gases; and thus
they are worked alternately, the action being constantly reversed after
suitable intervals.
When iron is combined with a much smaller proportion of carbon
than in cast iron, and contains little or no graphitic or uncombined
carbon, we have the very useful compound known as steel. In the earlier
half of the century it was customary to distinguish steel from malleable
iron on the one hand, and cast iron on the other. If the compound contained
from 0·5 to 1·5 per cent. of carbon, it was called steel by some
authorities, while others extended these limits a little on either side.
Later it was found that the presence of elements other than carbon can
confer steely properties on iron, and indeed it is possible to have a metal
containing no carbon, but possessing the characteristic properties of steel.
Sir Joseph Whitworth proposed to classify a piece of metal according to
its tensile strength, without any regard to either its chemical composition or
its mode of manufacture: if it could not bear more than 30 tons per square
inch it should be considered iron, but if it had a higher tensile strength,
it should then be regarded as steel. To estimate the engineering value
a figure depending upon the elongation or stretching of the specimen
before breaking was to be added to the number of tons of the breaking
load. This stretching power of steel is in some cases of as much importance
as the tensile strength: the ordnance maker, for instance, considers
a steel with a breaking strength of 53 tons under an elongation of 5 per
cent. as for his purposes to be rejected: while a specimen showing a
breaking strain of only 30 tons along with an elongation of 35 per cent., on
2 inches of length, he will regard as good. The tensile strength of steel
depends in part on its composition, in part on the mode of manufacture,
53and in part on the subsequent treatment. The average tensile strength
of a wrought iron bar per square inch of section is about 25 tons (30 is
the maximum); while the like average for steel is 43 tons, and some
kinds of cast steel will bear nearly 60 tons. Steel bars of a certain
temper subjected by Sir Joseph Whitworth to a process of hardening in
oil showed a tensile strength of even 90 tons per square inch. These
figures will suffice to show the great utility of steel in structures and
machines. But steel has besides a characteristic property which makes
it extremely valuable in a great variety of applications, namely, its capability
of being tempered. If a piece of steel is heated to dull redness and
suddenly cooled by plunging it into cold water, it becomes so extremely
hard that it cannot be acted on by a file; nay, its hardness may be made
to rival that of the diamond, which is the hardest substance known. Now
by a second operation this hardness can be reduced to any required
degree: this is done by re-heating the metal to a certain moderate degree
between 430° F. and 630° F. and again cooling it by immersion in some
cooling medium. In this “letting down” process, it is the highest temperature
that produces the greatest softening, and the properties of the
tempered steel will depend upon the precise degree to which the metal
has been reheated. For example, if the product be required for making
into sword blades, or watch-springs, and to possess much elasticity, the
proper temperature is between 550° F. and 570° F.; but if the steel is to
be suitable for saws the temperature must range within a few degrees of
600° F., according to the fineness of the tool intended; a lower temperature
would give a metal too hard for them to be sharpened with a file. On
the other hand, sharp cutting instruments and tools for working metals
are obtained hard by tempering at lower degrees than springs. In
practice the index of the temperature is taken from the colour of the film
of oxide that gradually forms on a polished surface of the metal as the
heat is raised, and begins by a very pale yellow (at 430° F.), passing
through deeper shades into brown, then through purple into deep blue
(at 570° F.), etc. The reader will now see why watch and clock springs
have their deep blue colour, and he can observe for himself the whole
series of colours by very gradually heating a piece of polished steel over
a small flame.
If we compare the chemical composition of wrought iron and of cast
iron with that of steel as regards the content of carbon, we see at once
that steel holds an intermediate position, so that if in the puddling
furnace we could arrest the decarbonization at a certain point we should
obtain steel; or if, on the other hand, we could put back into chemical
combination with the decarbonized wrought iron a due percentage of
carbon we should in that way also obtain steel. And it will be observed
that the oldest primitive furnaces could not have failed sometimes to have
produced steel as the net or final result of such actions. In fact, steel
always has been and still is produced on one or other of these two
principles, applied in divers ways, but severally and distinctly directed
to that end. Of the many more or less modified processes of steel-making
that have been in use, we need here but briefly mention a few which
were the processes of the first sixty years of our century, and are to a
considerable extent still in operation, although eclipsed in importance
by two other processes that, since the date referred to, have been supplying
the metal in enormously increased quantities, and which will have
to be particularly described.
54The most usual of the older processes of steel-making, still carried on
at Sheffield and elsewhere, is known as the cementation process: it
consists in heating bars of the best wrought iron in contact with charcoal,
at a high temperature, for three or four weeks. At Sheffield the iron bars
and charcoal are packed in alternate layers into troughs 14 ft. long by
3½ ft. deep and wide, constructed of slabs of siliceous sandstone 6 in.
thick. The last layer of charcoal at the top is covered to a certain depth
with a layer of refractory matter, and the flames from a furnace beneath
are made to envelop the stone troughs or pots, as they are technically
called, for a period of a week or more according to the thickness of the
bars operated upon. These are generally 3 in. broad and from five- to
six-eighths of an inch thick. When it is found by withdrawing a test
bar for examination that the operation is complete, the fire is gradually
diminished and the whole allowed to cool slowly, which requires about a
fortnight. Instead of only charcoal, a mixture of powdered charcoal or
soot with a little salt has been used by some makers—which mixture,
technically called cement powder, has given its name to the process. In
some works 16 tons or more of iron are treated in one operation. The
bars are found unchanged in form, but increased in weight by perhaps
27 lbs. per ton, for carbon has combined with the iron, being apparently
transferred in the iron from one particle to another. The surface of the
bars becomes rough and uneven from a multitude of blebs or blisters,
and hence they are called blister bars, and the steel of which they now
consist is named blister steel. In this conversion we may suppose that
the iron at its outer surface first enters into combination with carbon
taken from the carbonic oxide gas, which would be produced by combustion
of the charcoal with the limited quantity of air in its interstices,
and the oxygen thus set free would immediately seize again on the
surrounding charcoal, and by repeated changes of this kind in which the
oxygen acts as a carrier of carbon to the iron, in which it is transferred
inwards from particle to particle. The cause of the blisters has been
much discussed: probably the cause is the formation and escape of a
volatile compound of carbon and sulphur at the surface of the soft metal;
for it is known that nearly the whole of the little sulphur in the wrought
iron disappears in the cementation process. Blister steel is never homogeneous,
for near the surface it always contains more carbon than within;
the bars are therefore broken up into short lengths which are carefully
assorted, bound together with wire, heated, welded together under a
hammer or by rolling, and finally formed into a bar, which is stamped
with the outline of a pair of shears, and is then known as shear steel,
because this product was generally found the most suitable for making
the shears used in dressing cloth.
Another method of dealing with the blister steel is to charge crucibles
or pots having covers with 50 or 100 lbs. weight of the broken-up bars, and
subject the crucibles to a strong heat in a reverberatory furnace, when the
metal melts, and at the proper moment the contents of a great number
of pots are almost simultaneously poured into a mould to form an ingot.
The result is a very uniform steel of the finest texture, known and highly
esteemed as cast steel or crucible steel. This steel is much more fusible
than iron, but less so than cast iron.
The production of steel by arresting at a certain stage the decarbonizing
of cast iron in the puddling furnace requires much experience on
the part of the workman, who has to learn when the desired point has
55been reached by certain indications, such as the appearance of the flame,
or by the examination of a small sample of the fluid metal withdrawn
and rapidly cooled. Various additions to the charge in definite proportions
are generally made, such as scales of iron oxide, or a quantity of
an oxide ore (hæmatite, etc.) or other materials, the most essential for a
good product consisting of a little manganese in some form. The result
is puddled steel; and this, like blister steel, can be converted into cast
steel by fusion in crucibles, running into ingot moulds, and subsequent
treatment by hammering, pressing, rolling, etc. In 1864 puddled steel
was described as an article of great commercial importance, but this it
soon lost by the introduction of simpler, cheaper, and more reliable
processes. The methods and improvements proposed for the production
of steel have been exceedingly numerous, as is shown by the records of
the English Patent Office alone, which contain up to the end of 1856
specifications of ninety-two patents for different steel-manufacturing processes,
while from 1857 to 1865, the epoch-marking period of steel
making, seventy-four more patents were obtained for this purpose. It
would be quite beyond our limits to make special reference to these, and
to the numerous patents which have since been granted, but there is one
of great importance in steel-making which must be mentioned, and that
is the patent for the employment in the cementation process of carbide of
manganese, taken out by J. M. Heath in 1839. This made England
almost independent of the former large importations of Swedish and
Russian iron, and it caused an immediate reduction of £40 in the price per
ton of good steel, effecting a saving which up to 1855 is calculated at not
less than £2,000,000. Heath was one of those who fail to benefit by their
inventions, for his was boldly appropriated by another person who took
advantage of a verbal flaw in the specification, and Heath did not obtain
any redress from the law courts until, after ten years’ litigation, a majority
of Exchequer judges reversed all the previous decisions against him
(1853). In the meantime the man had died, but as the patent was about
to expire his widow was on petition granted an extension of it for
seven years. The nature of the influence of manganese on steel-making
has not been fully explained, and there is some diversity of opinion on
the subject, as it is said—on the one hand, merely to remove or counteract
the injurious effects of sulphur or phosphorus; on the other, to impart to
the steel greater ductility, strength, and power of welding, tempering, etc.
The manufacture of crucible or cast steel has been carried on at Essen
in Prussia by the firm of A. Krupp & Co., on a scale surpassing anything
attempted elsewhere,—theirs being the largest steel-works in the world,
and remarkable for the variety and excellence of its products. It began
in so small a way that it is said only a single workman was employed.
To the Great Exhibition of 1851, at London, Krupp’s firm sent a block of
crucible cast steel weighing 2¼ tons, a larger mass of the metal than had
ever been shown before, and looked upon with no little astonishment, for
at that time steel was a precious commodity, the price of refined steel
ranging from £45 to £60 per ton. At the next London Exhibition, in
1862, the Essen Works showed a block of cast steel 20 tons in weight,
and at the Vienna Exhibition of 1873, one of 52 tons. This casting, which
was first made of a cylindrical shape, was forged into an octagonal form
under an immense steam-hammer, larger than the Woolwich hammer
described on a previous page, for the weight of the moving part is no less
than 50 tons. This huge mass of cast steel was of the finest quality; the
56forging into the prismatic form was to show its malleability, for it was
intended for the body of a gun to have a bore of 14 inches. Since the
period referred to, ingots of more than 100 tons have been cast. That
shown at Vienna was the product of some 1,800 crucibles, each containing
65 lbs. of melted steel, which had to be poured into the mould in a regular
and continuous stream, so that the metal might solidify into a perfectly
uniform mass. Such work can be done only by trained men, who act in
regular ranks with military precision, and in pairs emptying their crucibles
into channels previously assigned, then filing off to the other end of the
rank to receive another crucible, while the pair of men who were behind
are pouring out theirs, and so on in succession. The crucibles are emptied
into a number of channels formed of iron lined with fire-clay, and leading
down into the mould. Many precautions have to be taken to ensure the
regular progress of the operations, and all the time required to fill the
huge moulds may be counted by minutes.
The headpiece to our chapter on Fire-Arms gives but a very inadequate
idea of the magnitude of the Essen Works about 1870. A better
notion will be obtained from a few figures which we select from a list
giving some of the contents of the Essen Works in 1876. There were
1,109 furnaces of various kinds, of which 250 were for smelting; 77 steam
hammers, 294 steam engines, 18 rolling mills, 365 turning lathes, and 700
other machine tools; 24 miles of ordinary gauge railway for traffic within
the works; together with 10 miles of narrow gauge railway; 38 miles of
telegraph lines, with 45 Morse apparatus, etc. (J. S. Jeans’ Steel: its
History, etc., 1880). These figures belong, be it observed, to the state
of things in 1876; but we learn from a later authority that in 1894 these
works employed 15,000 men, and we must suppose that the plant has
been proportionately increased since the earlier period, when 10,000 men
were employed.
In the year 1854 a regular system of records began to be kept of the
amounts of coal and ores raised in Great Britain, and also of the quantities
of the various metals produced. These show that in 1894 very nearly
three times as much coal was raised as in 1854, and that in the same period
the quantity of British pig iron smelted annually had increased four-fold;
these increases look small when compared with the expansion of the
steel production in Britain within the same period of forty years, for this
had enlarged thirty-fold. This extraordinary development is attributable
to the introduction of two processes by either of which various steels of
excellent quality, and adapted to a great range of applications, can be
produced cheaply and with certainty. These processes are respectively
known as the Bessemer and the Open Hearth, and the reader should
observe that with the main principles involved in these he has already
been made acquainted.
Henry Bessemer, who first saw the light in England in 1813, may be
said to have been born an inventor, for his father was one before him—a
Frenchman employed in the royal mint at Paris, afterwards appointed
by the Revolutionary authorities to superintend a public bakery; on an
accusation of giving short weight, thrown into prison, from which, and
probably from the guillotine, he escaped, and found employment in the
English mint. Subsequently he devised some notable improvements in
the art of producing letterpress type, and for many years carried on a
prosperous business as a typefounder. The son developed inventive
faculties at a very early age: in lathe engraving, dies, dating stamps,
57etc. His name became familiar to everyone by his production of the
metallic powder long known as “Bessemer’s Gold Paint.” It became
known to Bessemer that the raw material of this substance, which was
then sold at £5, 10s. per lb., really cost only about one shilling per lb.,
and he set himself to discover its composition and mode of manufacture.
He succeeded in this so well that he could produce the article at the
insignificant cost of four shillings a pound, and his first order for a supply
of it was at the rate of £4 per lb., and the business was continued, realising
profits of something like 1,000 per cent. at first. For this article no
patent was taken out, but Bessemer himself, assisted by two trustworthy
workmen, carried on the manufacture in secret, and he some time afterwards
rewarded the fidelity of his men by handing over the business to
them as a free gift. Then he took out patents for improvements in the
manufacture of oils, varnishes, sugar, plate glass, etc. Several of his
machines for these purposes were shown at the London Exhibition of
1851. Bessemer is said to have obtained altogether some 150 patents,
including those granted for inventions connected with our subject. He
may be regarded as the type of the very fortunate inventor, since
on the patents of the one process we are going to describe he
ultimately obtained royalties to the value of more than £1,057,000,
and this irrespective of profits derived from commercially working it
himself.
At the time of the Crimean War, Bessemer had some experiments made
at Vincennes with cylindrical projectiles he had devised for firing from
smooth-bore guns, yet so as to impart to the projectile at the same time
rotation about its axis. The experiments were successful, but it was
pointed out that the guns of cast iron then in use would not bear heavy
projectiles, and he was induced, at the suggestion of the Emperor
Napoleon III., to undertake some researches with the view of finding metal
more suitable for artillery. Bessemer, having then little knowledge of
the metallurgy of iron, applied himself on his return to England to the
study of the best books on the subject, visited the principal iron-working
districts, and began a series of experiments at a small experimental installation
he set up in London. There, after repeated failures, he did at
length succeed in producing a metal much tougher than the cast iron
then used, and a small model gun was submitted to the Emperor, who
encouraged Bessemer to persevere with his experiments; which he did,
though the expense was a great tax on his capital, continued as the experiments
were for two years and a half. But by this time he had acquired
a knowledge of many important facts, and these gradually led him to the
experimental realization of the idea he had conceived, but only after many
trials in which several thousand pounds were expended. At length the
agenda of the British Association for the Cheltenham meeting of 1856
announced that a paper would be read by H. Bessemer, entitled
“The Manufacture of Iron and Steel without Fuel.” It will be easily
understood that a title in such terms would give rise to much derisive
incredulity; and we may imagine the iron-masters on that occasion
crowding into Section G, while asking each other in the spirit of certain
philosophers of old, “What will this babbler say?” Some of what he
did say may here be quoted, as at once explanatory and historically
memorable.
“I set out with the assumption that crude iron contains about 5 per
cent. of carbon; that carbon cannot exist at a white heat in the presence
58of oxygen without uniting therewith and producing combustion; that
such combustion would proceed with a rapidity dependent on the amount
of surface of carbon exposed; and lastly, that the temperature which the
metal would acquire would be also dependent on the rapidity with which
the oxygen and carbon were made to combine; and consequently, that
it was only necessary to bring the oxygen and carbon together in such a
manner that a vast surface should be exposed to their mutual action, in
order to produce a temperature hitherto unattainable in our largest
furnaces.
Fig. 23.—Experiments at Baxter House.
“With a view of testing practically this theory, I constructed a cylindrical
vessel of 3 ft. in diameter and 5 ft. in height, somewhat like an
ordinary cupola furnace (see Fig. 23). The interior is lined with firebricks,
and at about 2 in. from the bottom of it I inserted five tuyère
pipes, the nozzles of which are formed of well-burned fire-clay, the orifice
of each tuyère being about three-eighths of an inch in diameter; they are
so put into the brick lining (from the outer side) as to admit of their
removal and renewal in a few minutes, when they are worn out. At one
side of the vessel, about half-way up from the bottom, there is a hole
made for running-in the crude metal, and on the opposite side there is a
tap-hole, stopped with loam, by means of which the iron is run out at the
end of the process. In practice this converting vessel may be made of
any convenient size, but I prefer that it should not hold less than one
nor more than five tons of fluid iron at each charge; the vessel should
59be placed so near to the discharge hole of the blast furnace as to allow
the iron to flow along a gutter into it. A small blast cylinder is required
capable of compressing air to about 8 lbs. or 10 lbs. to the square inch.
A communication having been made between it and the tuyères before
named, the converting vessel will be in a condition to commence work;
it will however on the occasion of its first being used after re-lining with
firebricks be necessary to make a fire in the interior with a few baskets
of coke, so as to dry the brickwork and heat up the vessel for the first
operation, after which the fire is to be all carefully raked out at the
tapping-hole, which is again to be made good with loam: the vessel will
then be in readiness to commence work, and may be so continued without
any use of fuel until the brick lining, in the course of time, becomes
worn away, and a new lining is required. I have before mentioned that
the tuyères are situated nearly close to the bottom of the vessel, the fluid
metal will therefore rise some 18 in. or 2 ft. above them; it is therefore
necessary, in order to prevent the metal from entering the tuyère
holes, to turn on the blast before allowing the fluid crude iron to run into
the vessel from the blast furnace. This having been done, and the metal
run in, a rapid boiling up of the metal will be heard going on within the
vessel, the metal being tossed violently about and dashed from side to
side, shaking the vessel by the force with which it moves; from the throat
of the converting vessel flame will immediately issue, accompanied by a
few bright sparks such as are always seen rising from the metal when
running into the pig-beds. This state of things will continue for about
fifteen minutes, during which time the oxygen in the atmospheric air
combines with the carbon contained in the iron, producing carbonic
oxide, or carbonic acid gas, and at the same time evolving a powerful
heat. Now, as this heat is generated in the interior of, and is diffused in
innumerable fiery bubbles through, the whole fluid mass, the metal absorbs
the greater part of it, and its temperature becomes immensely increased,
and by the expiration of the fifteen minutes before named that part of
the carbon which appears mechanically mixed and diffused throughout
the crude iron has been entirely consumed: the temperature however is so
high that the chemically combined carbon now begins to separate from the
metal, as is at once indicated by an immense increase in the volume of
flame rushing out of the throat of the vessel. The metal in the vessel
now rises several inches above its natural level, and a light frothy slag
makes its appearance and is thrown out in large foam-like masses. This
violent eruption of cinder generally lasts about five or six minutes, when
all further appearance of it ceases, a steady and powerful flame replacing
the shower of sparks and cinder which always accompanies the boil.
The rapid union of carbon and oxygen which thus takes place adds still
further to the temperature of the metal, while the diminished quantity of
carbon present allows a part of the oxygen to combine with the iron,
which undergoes combustion and is converted into an oxide. At the
excessive temperature that the metal has now acquired, the oxide as
soon as formed undergoes fusion, and forms a powerful solvent of those
earthy bases that are associated with the iron; the violent ebullition
which is going on mixes most intimately the scoria and metal, every part
of which is thus brought in contact with the fluid oxide, which will thus
wash and cleanse the metal most thoroughly from the silicon and other
earthy bases which are combined with the crude iron, while the sulphur
and other volatile matters which cling so tenaciously to iron at ordinary
60temperatures are driven off, the sulphur combining with the oxygen and
forming sulphurous acid gas.
“The loss in weight of crude iron during its conversion into an ingot
of malleable iron was found, on a mean of four experiments, to be 12½ per
cent., to which will have to be added the loss of metal in the finishing
rolls. This will make the entire loss probably not less than 18 per cent.
instead of about 28 per cent., which is the loss on the present system. A
large portion of this metal is however recoverable by heating with carbonaceous
gases the rich oxides thrown out of the furnace during the
boil. These slags are found to contain innumerable small grains of
metallic iron, which are mechanically held in suspension in the slags and
may be easily recovered.
“I have before mentioned that after the boil has taken place a steady
and powerful flame succeeds, which continues without any change for
about ten or twelve minutes, when it rapidly falls off. As soon as this
diminution of flame is apparent the workman will know that the process
is completed, and that the crude iron has been converted into pure malleable
iron, which he will form into ingots of any suitable size and shape by
simply opening the tap-hole of the converting vessel and allowing the
fluid malleable iron to flow into the iron ingot moulds placed there to
receive it. The masses of iron thus formed will be free from any
admixture of cinder, oxide, or other extraneous matters, and will be far
more pure and in a forwarder state of manufacture than a pile formed of
ordinary puddle bars. And thus it will be seen that by a single process,
requiring no manipulation or particular skill, and with only one workman,
from three to five tons of crude iron pass into the condition of several
piles of malleable iron in from thirty to thirty-five minutes, with the
expenditure of about a third part the blast now used in a finery furnace,
with an equal charge of iron, and with the consumption of no other fuel
than is contained in the crude iron.
“To those who are best acquainted with the nature of fluid iron, it may
be a matter of surprise that a blast of cold air forced into melted crude
iron is capable of raising its temperature to such a degree as to retain it
in a perfect state of fluidity after it has lost all its carbon and is in the
condition of malleable iron, which, in the highest heat of our forges, only
becomes softened into a pasty mass. But such is the excessive temperature
that I am enabled to arrive at with a properly shaped converting
vessel and a judicious distribution of the blast, that I am enabled not
only to retain the fluidity of the metal, but to create so much surplus
heat as to remelt all the crop-ends, ingot-runners, and other scrap that is
made throughout the process, and thus bring them, without labour or
fuel, into ingots of a quality equal to the rest of the charge of new
metal....
“To persons conversant with the manufacture of iron, it will be at once
apparent that the ingots of the malleable metal which I have described
will have no hard or steely parts, such as are found in puddled iron,
requiring a great amount of rolling to blend them with the general mass,
nor will such ingots require an excess of rolling to expel cinder from the
interior of the mass, since none can exist in the ingot, which is pure and
perfectly homogeneous throughout, and hence requires only as much
rolling as is necessary for the development of fibre; it therefore follows
that, instead of forming a merchant bar, or rail, by the union of a number
of separate pieces welded together, it will be far more simple and less
61expensive to make several bars or rails from a single ingot. Doubtless
this would have been done long ago had not the whole process been
limited by the size of the ball which the puddler could make.
“The facility which the new process affords of making large masses
will enable the manufacturer to produce bars that, in the old mode of
working, it was impossible to obtain; while at the same time it admits of
the use of more powerful machinery, whereby a great deal of labour will
be saved and the process be greatly expedited.... I wish to call the
attention of the meeting to some of the peculiarities which distinguish
cast steel from all other forms of iron, viz., the perfectly homogeneous
character of the metal, the entire absence of sand-cracks or flaws, and its
greater cohesive force and elasticity, as compared with the blister steel
from which it is made,—qualities which it derives solely from its fusion
and formation into ingots, all of which properties malleable iron acquires
in like manner by its fusion and formation into ingots in the new process;
nor must it be forgotten that no amount of rolling will give the blister
steel, although formed of rolled bars, the same homogeneous character
that cast steel acquires by a mere extension of the ingot to some ten or
twelve times its original length....
“I beg to call your attention to an important fact connected with the
new process which affords peculiar facilities for the manufacture of cast
steel. At that stage of the process immediately following the boil the
whole of the crude iron has passed into the condition of cast steel of
ordinary quality. By the continuation of the process the steel so produced
gradually loses its small remaining portion of carbon, and passes
successively from hard to soft steel, and from soft steel to steely iron, and
eventually to very soft iron; hence, at a certain period of the process, any
quality of metal may be obtained. There is one in particular which by
way of distinction I call semi-steel, being in hardness about midway
between ordinary cast steel and soft malleable iron. This metal possesses
the advantage of much greater tensile strength than soft iron; it is also
more elastic, and does not readily take a permanent set, while it is much
harder and is not worn or indented so easily as soft iron; at the same
time it is not so brittle or hard to work as ordinary cast steel. These
qualities render it eminently well adapted to purposes where lightness
and strength are specially required, or where there is much wear, as in
the case of railway bars, which from their softness and lamellar texture
soon become destroyed. The cost of semi-steel will be a fraction less
than iron, because the loss of metal that takes place by oxidation in the
converting vessel is about 2½ per cent. less than it is with iron; but as it
is a little more difficult to roll, its cost per ton may fairly be considered to
be the same as iron; but as its tensile strength is some 30 or 40 per cent.
greater than bar iron, it follows that for most purposes a much less weight
of metal may be used than that so taken. The semi-steel will form a
much cheaper metal than any we are at present acquainted with. These
facts have not been elicited from mere laboratory experiments, but have
been the result of working on a scale nearly twice as great as is pursued in
our largest iron works, the experimental apparatus doing 7 cwt. in thirty
minutes, while the ordinary puddling furnace makes only 4½ cwt. in two
hours, which is made into six separate balls, while the ingots or blooms
are smooth, even prisms, 10 in. square by 30 in. in length, weighing
about equal to ten ordinary puddle balls.”
The startling novelty of the methods and results described in this
62paper had the effect of paralyzing discussion at the time. But soon the
voice of detraction was heard; many iron-masters ridiculed the idea of
producing iron and steel without fuel, and indeed it may have been
observed, the title of the paper notwithstanding, that first the silicon and
carbon, and then the iron itself, really supplied the fuel. And we must
remember that malleable iron in a molten state was then deemed an
impossibility, for the hottest furnaces then known could not effect the
fusion, however prolonged their action might be, yet Bessemer was to
obtain five tons in this condition in the short space of half an hour with
no other aid than cold air. Then it was said that Bessemer’s process of
forcing air into melted cast iron had no claim of novelty, for it had been
tried before and found valueless. Some iron-masters on trying experiments
on a small scale and with imperfect appliances met with failures,
and discredited the process at once; but five large establishments paid
for licences sums amounting to £26,500 within three weeks of the reading
of the paper. At the works of the Dowlais Iron Co., in South Wales,
who were the first licensees, the first converter was set up under
Bessemer’s personal superintendence, and at the first operation five tons
of iron were produced direct from the blast furnace pig. This apparently
satisfactory result proved quite otherwise when this iron came to be
practically tested; for it was found quite useless! It was both “cold-short”
and “red-short,” to use the technical terms,—the former of which
means that although the sample may be welded, it is when cold brittle
and rotten; the latter means that at a low red heat it breaks and
crumbles under the hammer. Further trials were made, new experiments
instituted, but the success that attended Bessemer’s early experiments
could not be repeated, and as yet no one knew the reason why. Now it
so happened that in the preliminary experiments an exceptionally pure
pig iron had been made use of containing little or no phosphorus or
sulphur, substances very deleterious in iron, and still more so in steel.
With the capital obtained by the sale of his licences Bessemer quietly
set to work to investigate the cause of his non-success, making daily
experiments with a ton or two of metal at a time. These experiments
extended over a period of two and a half years, and upon them
Bessemer and his partner spent about £16,000, besides the £4,000 the
preliminary researches had cost. But all difficulties were at length overcome,
and the process was now found capable of turning out pure iron
and steel when the pure pig iron of Sweden was used in the converter.
In the meantime the licensees had made no attempts practically to
carry out the process, which began to be denounced as visionary: it
was “a mare’s nest”; it was “a meteor that had passed through the
metallurgical world, but had gone out with all its sparks.” When
Bessemer again brought the subject before the public, he found that no
one believed in it; everyone said, “Oh, this is the thing that made such
a blaze two or three years ago, and which was a failure.” Neither iron-makers
nor steel-makers would now take it up. Bessemer and his
partner thereupon joined with three other gentlemen to establish at
Sheffield a steel-works of their own, where the invention should be
carried into full practice. In due time works were erected, and they
commenced to sell steel, receiving at first very paltry orders, for such
quantities as 28 lbs. or 56 lbs.; but the orders soon became larger, and
afterwards very much larger, for they were underselling the Sheffield
manufacturers by £20 a ton, and their steel was undistinguishable from
63the higher priced article. Bessemer had now bought his licences back
again, and in the course of his second set of experiments had patented
each improvement as it occurred to him, finally bringing the mechanical
apparatus to the degree of efficiency requisite for practical working, without
which his primary idea would have been valueless. Before directing the
reader’s attention to the form the apparatus had assumed, we may transcribe
what Mr. Jeans, in the work above referred to, has told about the
commercial success of the Bessemer steel-making firm:—
“On the expiration of the fourteen years’ term of partnership of this
firm the works, which had been greatly increased from time to time out
of revenues, were sold by private contract for exactly twenty-four times
the amount of the whole subscribed capital, notwithstanding that the firm
had divided in profits during the partnership a sum equal to fifty-seven
times the gross capital, so that by the mere commercial working of the
process, apart from the patent, each of the five partners retired after
fourteen years from the Sheffield works with eighty-one times the
amount of his subscribed capital, or an average of nearly cent. per cent.,
every two months,—a result probably unprecedented in the annals of
commerce.”
Fig. 24.—Bessemer Converter.
A, Front view, showing the mouth, c; B, Section.
The form of the Bessemer apparatus as it finally left the inventor’s
hands may now be considered: but in certain details and arrangements
some modifications, dictated by the experience and requirements of
individual establishments, have been made, leaving the principles of the
apparatus unchanged. Thus instead of making the converting vessel
turn on trunnions, it is sometimes constructed fixed, the fluid metal after
conversion being let out at a tap-hole; the number and size of the
tuyères are varied; and so with the disposition of the air chamber or
tuyère box, the pressure of the blast, the capacity of the converter itself,
etc. In capacity converters vary between 2½ tons and 10 tons; one of
medium size is shown in elevation and section in Fig. 24, and may
64be described as an egg-shaped vessel about 15 ft. high and 6 ft.
diameter inside. It is strongly made of wrought iron in two parts bolted
together, and is lined inside with some thick infusible coating, of which
more is to be said presently. The converter swings on trunnions, one of
which is hollow, and admits the blast by the pipe b to the base of the
vessel, whence it passes through the passages shown at e. The thickness
of the lining at e may perhaps be 20 in., and passages for the air are
perforated in fire-clay tuyères, of which there may be seven, each with
seven perforations of half an inch diameter. To the other trunnion is
attached a toothed wheel which engages the teeth of a rack receiving
motion from hydraulic pressure. The iron for the operation is melted in
a furnace having its hearth above the level of the converter; and to
receive its charge the latter is turned so that the molten cast iron may be
poured in from a trough until its surface is nearly on a level with the
lowest of the tuyères. The blast having been turned on, the hydraulic
power is set to work and the converter is slowly brought to an upright
position. The pressure of the current of air prevents any of the fluid
metal from entering the blow-holes. The blast of cold air is continued
until all the silicon and carbon have been removed by oxidation. If the
production is to be steel, there is then added to the contents of the
converter, placed in position to receive it, a certain weight of melted
cast iron of a special constitution, and the blow is resumed for a few
minutes; or in more recent practice this special metal is added to the
fluid metal run out of the converter into a spacious ladle in known
quantity. On this addition an intense action takes place, attended by an
extremely brilliant flame and a throwing out of cinder or slag. The
metal thus added to the decarbonized iron is a carbonized alloy of iron
and manganese obtained from an ore naturally containing the latter
metal, and scarcely any phosphorus or sulphur. The charcoal pig from
this ore is called spiegeleisen (German = mirror-iron) from its brilliant
reflecting facets; it contains from 12 to 20 per cent. of manganese, with
about 5 per cent. of carbon, and a considerable proportion of silicon.
An exact chemical analysis of the particular spiegeleisen having been
previously made, it is known what proportion of it is to be added to the
decarbonized iron in order to convert this into a steel with any required
content of carbon. The manganese probably acts by combining with
oxide of iron diffused through the mass, and together with the silicon
forming the very easily separated slag which is ejected.
The whole series of operations connected with the Bessemer process
may be easily followed by the help of Fig. 25, which is taken from a
beautiful model in the Museum of Practical Geology. This model, which
was presented to the museum by Mr. Bessemer himself, represents every
part of the machinery and appliances of the true relative sizes. C is the
trough, lined with infusible clay, by which the liquid pig iron is conveyed
to the converters, A. The hydraulic apparatus by which the vessels are
turned over is here below the pavement, but the rack which turns the
pinion on the axis of the converter is shown at B. The vessel into which
the molten steel is poured from the converter is marked E, and this vessel
is swung round on a crane, D, so as to bring it exactly over the moulds,
placed in a circle ready to receive the liquid steel, which on cooling is
turned out in the form of solid ingots. The valves which control the
blast, and those which regulate the movements of the converter through
the hydraulic apparatus, are worked by the handle seen at H. The
66crane, or revolving table, D, is also under perfect control, so that the
crude pig iron is converted into steel, and the moulds are filled with a
rapidity and ease that are positively marvellous to a spectator.
Fig. 25.—Model of Bessemer Steel Apparatus.
The development of the Bessemer process soon had the effect of so
reducing the price of steel that this material came into use for almost
every purpose for which iron had previously been employed, such as
railway bars, girders, etc., for bridges, boiler plates, etc., for all which
“steely iron” containing only 0·12 to 0·40 per cent. carbon proved
admirably adapted. The practical success of the Bessemer process had
not long been demonstrated commercially by the inventor and his
partners at Sheffield before other firms began the manufacture: so that
in 1878 there were in Great Britain alone twenty-seven establishments
making Bessemer steel and using 111 converters. It may give an idea
of the magnitude the Bessemer steel manufacture had attained even at
that time if we quote the cost of erecting a complete plant for two
5–ton converters: it was £44,400, as given in a detailed estimate. In all
these cases pig iron from ores free from phosphorus and sulphur had to
be used, for as we have seen the converter failed to eliminate these
vitiating elements. Imported pig ores had in general to be used, or
pig from the limited supply of British hæmatite ores in West Cumberland.
The Barrow Hæmatite Steel Company engaged in the production
of Bessemer steel on a very large scale, having by 1878 erected no fewer
than sixteen converters of the capacity of 6 tons each. In the meanwhile
many efforts were made to discover some method of eliminating
phosphorus, so that the ordinary qualities of British pig iron, and iron
derived in any part of the world from the coarse phosphorized ores,
might be available for the converter. Many of the methods then devised
proved correct in principle and feasible in practice; but as, for sundry
reasons, none of them came extensively into use, we need not here allude
to them further.
The solution of the problem was announced in 1879. Some years
before, G. J. Snelus had come to the conclusion that with a siliceous lining
it would be impossible to eliminate phosphorus in the Bessemer converter,
and that some refractory substance of a basic character must be sought
for in order that the slag produced should be in a condition to absorb
the phosphoric acid as fast as it is produced. He patented in 1872 the
use of magnesian limestone as a material for the lining; as that
substance when intensely heated became very hard and stony, being in
that condition quite unaffected by water. Two young chemists, Messrs.
Thomas and Gilchrist, apparently without being aware of Mr. Snelus’s
conclusions, had also convinced themselves that the chief deficiency in
the Bessemer process was due to the excess of silica in the slag, and in
1874 they began to try the effect of basic linings, and also of basic
additions, such as lime, etc., to the charge in the converter, so that the
lining itself should not be worn out by entering into the slag. Their
results proved that phosphorus could be eliminated when the slag
contained excess of a strong base. An example of an operation at
Bolckow, Vaughan, & Company’s Eston works with the highly
phosphorized Cleveland pig iron may be quoted. The basic-lined converter
received first 9 cwt. of lime, then 6 tons of metal. When the blast
at 25 lbs. pressure was turned on, the silicon began at once to burn; for
three minutes the carbon was not affected, but for fourteen minutes
longer it regularly diminished, the silicon keeping pace with it. After
67the blow had been continued for thirteen minutes from the commencement,
the converter was turned down to allow of the further introduction of
19½ cwt. of a mixture of two parts of lime with one of oxide of iron. So
long as 1·5 per cent. of carbon remained in the metal the phosphorus
was untouched, and at the end of the blow, i.e. when the flame dropped,
only one-third of it had been eliminated; it still formed 1 per cent. of the
metal. The blast continued for another two minutes brought it down to
¼ per cent., and in one more minute only a trace was left. Most of the
sulphur was got rid of at the same time. From Cleveland pig, thus
de-phosphorized in the Bessemer converter, large quantities of steel rails
were rolled for the North Eastern Railway Company, and were found
entirely satisfactory, being as good as those made from the Cumberland
hæmatite steel. This de-phosphorized process has been brought into
operation wherever phosphoric ores are dealt with, and it has been
applied with equal success in the “open hearth” furnaces, of which we
have now to speak.
All discoveries and all inventions may be traced back to preceding
discoveries and inventions in an endless series, and it is only by its
precursors that each in its turn has been made possible. If we take one
of the greatest marvels brought into existence at nearly the close of our
epoch, namely, “wireless telegraphy,” we may follow up links of a
chain connecting it with the recorded observations of an ancient Greek
(Thales) who flourished seven centuries before our era, and even these
may not have been original discoveries of his. And it will have been
gathered from what has already been said that steel must have been
produced, however unwittingly, at the earliest period at which man began
to reduce iron from its ores. So the very latest, and for many purposes
the most extensively practised, process of modern steel-making, brought
indeed to working perfection mainly by the perseverance and scientific
insight of two individuals, is the result of the observation and the
accumulated experience of former generations. The observations and
experience here alluded to are chiefly those that follow two lines: one
concerning the properties of the metal itself, the other relating to the
means of commanding very high temperatures on a great scale. On this
occasion we are able almost to lay a finger on some proximate links of the
chain. Réaumur, the French naturalist, made steel in the early part of
the eighteenth century by melting cast iron in a crucible, and in this
liquid metal he dissolved wrought iron, the product being, as the reader
will now easily understand, the intermediate substance, steel; and this
was obtained of course at a temperature which was incapable of fusing
wrought iron by itself. He published in 1722 a treatise on “The Art of
converting Iron into Steel, and of softening Cast Iron.” For this, and
certain other metallurgical discoveries, Réaumur received a life-pension
equivalent to about £500 per annum,—a treatment very different from
that dealt out by the British to Henry Cort. The action in Réaumur’s
crucible is precisely that used on the large scale in Siemens’ open hearth.
But this last became possible only when Siemens had worked out his
“regenerative stove” or heat accumulator, the development of an idea
suggested by a Dundee clergyman in 1817.
A general notion of the Siemens’ regenerative stove will have been
already gained from the account given before of its application to the
modern type of blast furnace. Of the inventor himself, C. William
Siemens, it may be observed that he was one of a family of brothers, all
68remarkable for their scientific attainments, and in many of his researches
and processes he was aided by his brothers Frederick and Otto. In our
article on “Electric Power and Lighting” there will be found some
notice of a few of Siemens’ inventions pertaining to those subjects. A
still more admirable invention of his is the electric pyrometer, an instrument
of the utmost utility for measuring, with an accuracy previously
unapproachable, the high temperature of furnaces, etc. Indeed there
are few departments of science, pure or applied, which have not been
enriched by the researches and contrivances of this distinguished man,
whose merits were acknowledged by the bestowal upon him of the highest
scientific and academical honours, and also of a title, for he became Sir
William Siemens.
Fig. 26.—Section of Regenerative Stoves and Open Hearth.
Siemens was much engaged from 1846 in conjunction with his brother
Frederick in experimental attempts, continued over a period of ten years,
at the construction of the regenerative gas furnace. At length, in 1861, he
proposed the application of his furnace to an “open hearth,” and during
the next few years some partial attempts to carry out his process were
made, and he himself had established experimental works at Birmingham
in order to mature his processes, while Messrs. Martin of Sireuil, in
France, having obtained licences under Siemens’ patents, gave their
attention to a modification of his process, by which they succeeded in
producing excellent steel. Siemens having in 1868 proved the practicability
of his plans by converting at his Birmingham works some old
phosphorized iron rails into serviceable steel, a company was formed, and
in 1869 the Landore Siemens’ Steel Works were established at Landore
in Glamorganshire, and a few years after, these had sixteen Siemens
69open hearth melting furnaces at work, giving a total output of 1,200 tons
of steel per week. The number of furnaces was subsequently increased.
Extensive works specially designed for carrying out the Siemens and the
Siemens-Martin process were shortly afterwards erected at other places,
as at Newtown, near Glasgow, Panteg in Wales, etc. In Great Britain
the open hearth process gradually gained upon the Bessemer, until in
1893, when the total output of both kinds amounted to nearly 3,000,000
tons, this was almost equally divided between them, and since that period
the steel made by the former has greatly surpassed in amount that made
by the latter.
How the regenerative stove, or heat accumulator, works, and how it is
applied in the open hearth process, the reader may learn by aid of the
diagram Fig. 26, in which however no representation of the disposition of
the parts in any actual furnace is given, nor any details of construction
beyond what is necessary to make the principle clear. On the right and
on the left of the diagram will be seen a pair of similar chambers which
are shown as partly below the level of the ground SS´, such being a usual
disposition. The outer walls of these chambers are thick and the interior
is entirely lined with the most refractory fire-bricks, of which also is formed
the partition in between each pair of compartments, as well as the passages
from the top of each opening on the furnace H. Each chamber or
compartment is filled with rows of fire-bricks, laid chequerwise so as to
leave a multitude of channels between. At the bottom of the chamber
on the left let us suppose atmospheric air to be admitted by the channels
A, A, A, and a combustible gas which we may take to be a mixture of
carbonic oxide with some hydrogen is admitted in the same way to the
second compartment on the left through the passages G, G, G. Supposing
the apparatus quite cold in the first instance, the gas would ascend into
the furnace H as shown by the arrows, because it might be drawn by an
up-draught in a chimney connected with the six chambers shown at the
bottom of the right, and it would also tend to rise up into the space H
by its lighter specific gravity, and there it could be set on fire, when a
volume of flame would pass across to the right, a plentiful supply of air
rushing in through the air chamber from A, A, A, and the products of the
combustion, mainly hot carbonic acid gas and hot nitrogen gas, in passing
through the right-hand chambers, would make the bricks in both
compartments very hot after a time, for the current would divide itself
between the two passages, as indicated by the divided arrow. We have
not shown the valves by which the workman is able, by merely pulling a
lever, to shut off the air supply from A, A, A, and of gas from G, G, G, and
put these channels into direct communication with the up-draught
chimney, at the same time supplying gas at G´, G´, G´, and air at A´, A´, A´.
These rise up among the now heated bricks each in its own compartment,
but mix where they enter the furnace H, now hot enough to set them on
fire, and the gaseous products of combustion, hotter now than before,
descend among the fire-bricks of the left-hand compartments, heating
them in turn. After another period, say half an hour, the valves are
again reversed, and again gas and air both heated burn in the space H,
and their products supply still more heat to the right-hand compartments.
And so the action may be continued with a great temperature each time
produced by the combustion of the combining bodies at increasingly
higher temperatures. Thus, if cold gas and air by combination give rise
to 500° of heat, when the same combine, at say the initial temperature of
70400°, the result would be a temperature of 900°; if burnt at this latter
degree, then 900° + 500° would be reached, and so on. It would seem
as if there were no limit to the temperatures obtainable in this way.
But the nature of the materials of which the furnace is constructed
imposes a limit, for even the most refractory matters yield at length, and
the working would come to an end by the fusing of the brickwork. The
diagram is a section through the length of the hearth (for it is usually
oblong in plan), and the low arch above H being exposed to the fiercest
heat, is formed of the most refractory “silica bricks,” that is, bricks
made of coarsely ground silica held together with a little lime; yet this
extremely resisting material is acted upon, and the arch has to be
renewed every few months or sometimes weeks. The hearth itself is
supported by massive iron plates, shown in the diagram by the thick lines,
above which is laid a deep bed L, of quartz sand or ganister, or where
required a basic lining, beaten hard down, and forming a kind of basin
with sides sloping down in all directions to a point immediately below
the centre of the fire-brick door D, where is the aperture for tapping,
stopped by a mixture of sand and clay until the metal is ready for
drawing off, when it runs outside into an iron spout lined with sand
and is received into the ingot moulds. B in the figure represents the
“bath,” as it is called, of molten metal, which, in the larger furnaces,
where 20 tons of metal is operated on at once, may occupy an area of
150 square ft.
It need hardly be mentioned that there has to be a certain adjustment
between the volumes of air and of gas that pass into the regenerative
stoves, in order that the best effect may be obtained. Besides the limit
of temperature occasioned by the nature of the materials, there is a
chemical reason why the regenerative stoves cannot increase the temperature
indefinitely. It is noticed that when the temperature of the
furnace has become very high indeed, the flame over the hearth assumes
a peculiar appearance, being interrupted by dark spaces. These are
attributable to what is called in chemistry “dissociation,”—in this
case the dissociation of carbonic acid gas, which by the heat alone
separates into carbonic oxide and oxygen gases. In the same way these
gases refuse to combine if brought together heated beyond a certain
temperature. This phenomenon of dissociation is a general one, for it is
found that for any pair of substances there is a characteristic range of
temperature above or below which they refuse to combine. The gas
used in these stoves is either unpurified coal gas, or that produced by
passing steam over red-hot coal or coke.
We have spoken of the Siemens and the Siemens-Martin open hearth
processes. In the latter a charge of pig iron, say 1½ tons, is first melted
on the hearth, then about 2 tons of wrought iron is added in successive
portions, and in like manner nearly as much scrap steel (i.e. turnings,
etc.), the final addition being half a ton of spiegeleisen containing 12 per
cent. of manganese. A furnace of corresponding dimensions will allow
of three charges every twenty-four hours. In the Siemens process it is
not wrought iron or steel scrap that is mainly used to decarbonize the pig,
but a pure oxide ore. This is thrown into the bath of molten metal in
quantities of a few cwts. at a time, when a violent ebullition occurs. When
samples of the metal and of the slag are found to be satisfactory, spiegeleisen
or ferro-manganese is added, and the charge is cast. This
process takes a rather longer time than the former, but gives steel of
71more uniform character. In both processes, phosphorus is oxidized at
the high temperature attained and passes into the slag, which last floats
of course on the molten metal and is from time to time tapped off as the
action proceeds.
Fig. 26a.—Rolling Mill.
Fig. 26a shows a rolling mill with what is called a “two-high” train for
finishing bars by passing them between the grooves cut in the rolls to
give the required section. The rolls in the illustration turn in one direction
only, and therefore the bars after emerging from the larger grooves
have to be drawn back over the machine and set into a smaller pair from
the same side. This inconvenience is avoided in the “three-high train,”
on which three rolls revolve, and the bars can be passed through them
from one side to the other alternately. The celerity with which a glowing
steel ingot is without re-heating converted into a straight steel rail 60 or
100 feet long, by passing a few times backwards and forwards between
the rolls, is very striking. These rolls are made of solid steel, and in
some cases have a diameter of 26 inches or more.
72
Everyone knows how much iron is used in those great engineering
structures that mark the present age, and of which a few examples will be
described in succeeding articles. One other feature of the nineteenth
century is the use of iron in architecture. Some have, indeed, protested
against the use of iron for this purpose, and would even deny the name of
architecture to any structure obviously or chiefly formed of that material.
Stone and wood, they say, are the only proper materials, because each
part must be wrought by hand, and cannot be cast or moulded; and
further, iron being liable to rust, suggests decay and want of permanence,
and these are characters incompatible with noble building. All this can
rest only on a relative degree of truth—as, for instance, machinery is
used to dress and shape both wood and stone, and the permanence of
even the latter is as much dependent on conditions as that of iron. Iron
used in architecture is hideous when applied in shapes appropriate only to
stone; but when it is disposed in the way suggested by its own properties,
and receives ornament suitable to its own nature, the result is harmonious
and graceful, and the structure may display beauties that could be attained
by no other materials. Be that as it may, the great and lofty covered
spaces that are required for our railway stations and for other purposes
could have been obtained only by the free use of iron, and everyone can
recall to mind instances of such structure not devoid of elegance, in spite
of the absence—the proper absence—of the Classic “orders” or Gothic
“styles.” The first notable instance of the application of iron on a
large scale was the erection of the “Crystal Palace,” in Hyde Park, for
the great Exhibition of 1851. It was taken down and re-erected at
Sydenham, and there it has become so well known to everyone that any
description of it is quite unnecessary in this place.
As another conspicuous example of what may be done with iron, the
Eiffel Tower at Paris may be briefly described.
The idea of erecting a tower 1,000 feet high was not of itself new.
It had been entertained in England as early as 1833, in America
in 1874, and in Paris itself in 1881. It has been reserved for M.
Gustave Eiffel, a native of Dijon, who commenced to practise as
an engineer in 1855, to realize this ambitious project. He has
long been occupied in the construction of great railway bridges and
viaducts, and in these he has adopted a system peculiar to himself of
braced wrought-iron piers without masonry or cast-iron columns. He
also was the first French engineer to erect bridges of great span without
scaffolding. In the Garabit viaduct he planned an arch of 541 feet,
crossing the Truyère at a height of nearly 400 feet above it. One result
of M. Eiffel’s studies in connection with these lofty piers was his proposal
to erect the tower for the Paris Exhibition of 1889. This proposal met
with great opposition on the part of many influential people in Paris—authors,
painters, architects, and others protesting with great energy
against the modern Tower of Babel, which was, as they said, to disfigure
and profane the noble stone buildings of Paris by the monstrosities of a
machine maker, etc. etc. The Eiffel Tower is now constructed, and no
one has heard that it has dishonoured the monuments of Paris, for it has
been instead a triumph of French skill, the glory of its designer, and the
wonder of the Exhibition.
73
Fig. 26b.—The Eiffel Tower in course of construction.
The tower rests on four independent foundations, each at the angle of a
square of about 330 feet in the side, and it may be noted that the two
foundations near the Seine had to be differently treated from the other
two, where a bed of gravel 18 feet thick was found at 23 feet below the
74surface, and where a bed of concrete, 7 feet thick, gave a good foundation.
The foundations next the river had to be sunk 50 feet below the
surface to obtain perfectly good foundations. Underlying the whole is a
deep stratum of clay; but this is separated from the foundations by a
layer of gravel of sufficient thickness. Above this are beds of concrete,
covering an area of 60 square metres, and on the concrete rests a pile of
masonry. Each of the four piles is bound together by two great iron bars,
25 feet long and 4 inches diameter, uniting the masonry by means of
iron cramps, and anchoring the support of the structure, although its
stability is already secured by its mere weight. The tower is of curved
pyramidal form, so designed that it shall be capable of resisting wind
pressure, without requiring the four corner structures to be connected by
diagonal bracing. The four curved supports are, in fact, connected with
each other only by girders at the platforms on the several stages, until at
a considerable length they are sufficiently near to each other to admit
the use of the ordinary diagonals. The work was begun at the end of
January, 1887, and M. Eiffel notes how the imagination of the workmen
was impressed by the notion of the vast height of the intended structure.
Not steel, but iron is the material used throughout, and the weight of it is
about 7,300 tons, without reckoning what is used in the foundations, and
in the machinery connected with the lifts, etc. It has long ago been
found that stone would be an unsuitable material for a structure of this
kind, and it is obvious that only iron could possibly have been used to
build a tower of so vast a height and within so short a space of time, for
it was completed in April, 1889. A comparison of heights with the loftiest
stone edifices may not be without interest. The highest building in Paris
is the dome of the Invalides, 344 feet; Strasburg Cathedral rises to 466
feet; the Great Pyramid to 479 feet; the apex of the spire in the recently
completed Cathedral at Cologne to 522 feet. These are overtopped by
the lofty stone obelisk the Americans have erected at Washington,
which attains a height of more than 550 feet. Such spires and towers
have been erected only at the cost of immense labour. But iron, which
can be so readily joined by riveting, lends itself invitingly to the skill of
the constructor, more particularly by reason of the wonderful tensile
strength it possesses. It is scarcely possible to convey any adequate idea
of the great complicated network of bracings by which in the Eiffel
Tower each standard of the columns is united to the rest to form
one rigid pile. The horizontal girders unite the four piers in forming
the supports of the first storey some 170 feet above the base. The
arches which spring from the ground and rise nearly to the level
of these girders are not so much intended to add to the strength
of the structure as to increase its architectural effect. The first
storey stands about 180 feet above the ground, and is provided with
arcades, from which fine views of Paris may be obtained. Here there are
spacious restaurants of four different nationalities. And in the centre of
the second storey (380 feet high) is a station where passengers change
from the inclined lifts to enter other elevators that ascend vertically to
the higher stages of the tower. On the third storey, 900 feet above the
ground, there is a saloon more than 50 feet square, completely
shut in by glass, whence a vast panorama may be contemplated.
Above this again are laboratories and scientific observatories, and,
crowning all, is the lighthouse, provided with a system of optical
apparatus for projecting the rays from a powerful electric light. This
76light has been seen from the Cathedral at Orléans, a distance of about
70 miles.
Fig. 26c.—The Eiffel Tower.
The buildings of the Paris Exhibition of 1889 are themselves splendid
examples, not only of engineering skill, but of good taste and elegant
design in iron structures and their decorations. The vast Salle des
Machines (machinery hall) exceeds in dimensions anything of the kind
in existence, for it is nearly a quarter of a mile long, and its roof covers
at one span its width of 380 feet, rising to a height of 150 feet in the
centre. This great hall is to remain permanently, as well as the other
principal galleries with their graceful domes.
The Eiffel Tower having proved one of the most striking features of the
great Paris Exhibition, and of itself a novelty sufficient to attract visitors
to the spot, and having, long before the Exhibition closed, completely
defrayed the expense of its construction, with a handsome profit besides,
its success has naturally provoked similar enterprises,—as, for instance, at
Blackpool, a seaside resort in Lancashire, there has been erected an openwork
metal tower, resembling the Paris structure, but of far less altitude.
In several of the great cities of the United States, the last few years
have witnessed a novel and characteristic development of the use of iron
in architecture. In many structures on the older continent, this material
has been frankly and effectively employed, forming the obvious framework
of the erection, even when the leading motive was quite other than a display
of engineering skill. The Crystal Palace at Sydenham and other
erections have been referred to, in which iron has taken its place as the
main component of structures designed more or less to fulfil æsthetic
requirements: the guiding principle in “tall office buildings” in the cities
of the Western continent is, on the contrary, avowedly utilitarian. Iron
has, of course, long been used in the form of pillars, beams, etc., in
ordinary buildings, and it is only the extraordinary extension of this
employment of it, after the lift or elevator had been perfected, and
the ground-space in great commercial centres was daily becoming more
valuable, that has led to the erection of structures of the “sky-scraper”
class in American cities. For a given plot at a stated rent, a building of
many stories, let throughout as offices, will obviously bring to its owner a
greater return than one of few stories. The elevators now make a tenth
story practically as accessible as a third storey, and the tall building readily
fills with tenants. No claim for artistic beauty has been advanced for
these structures, which aim simply at being places of business, and if provision
be made for sufficient floor-space and daylight, and for artificial
lighting, heating, and ventilation, together with the ordinary conveniences
of modern life, and ready elevator service, nothing more is required by
the utilitarian spirit, that seeks only facilities for money-getting. These
tall buildings are usually erected on plots disproportionately small, and
the architectural effect is apt to be bizarre and incongruous, especially
when the structure shoots up skyward in some comparatively narrow
street amid more modest surroundings. They are really engineering
structures, but invested with features belonging to edifices of quite another
order of construction. If they are necessities of the place and period, and
are “come to stay,” it cannot be doubted but that decoration of an appropriate
78and harmonious character will, in course of time, be evolved along
with them, when the conventionality that clings to architecture shall be
broken through, and a new style appear, as consistent, and therefore as
beautiful, in relation to the “tall office building,” as were those of the
Greek temple and the Gothic minster in their free and natural adaptation.
PLATE IV.
THE AMERICAN TRACT SOCIETY BUILDING.
Fig. 26d.—St. Paul Building, N. Y.
Here, apparently, is the opportunity for the advent of a new and characteristic
style. There is great ingenuity displayed in the arrangement
and internal finish of these buildings. But besides the somewhat novel
application of iron, the most notable circumstances regarding them are the
tendency to make them of greater and greater height, and the wonderfully
short time in which, upon occasion, they can be run up. Chicago has
recently been noted for its tall edifices, among which may be named The
Reliance Building, erected upon a site only 55 feet in breadth, but rising
in fourteen stories to the height of 200 feet, and presenting the appearance
of a tower. There are no cast iron pillars, but the whole metal framework
is of rolled steel, the columns consisting of eight angle-sections,
bolted together in two-story lengths, adjoining columns breaking joint
at each floor, and braced together with plate girders, 24 inches deep,
bolted to the face of the columns, with which they form a rigid connection.
Externally, the edifice shows nothing but white enamelled terra-cotta and
plate glass. This building was originally a strongly-built structure of
five stories, the lower one being occupied as a bank. The foundations
and the first story were taken out, and prepared for the lofty edifice, the
superstructure being the while supported on screws. Then the three
upper stories were taken down, and the building was continued from the
second story, which was filled with tenants while the building was in
course of erection above.
Fig. 26e.—Manhattan Insurance Co.’s Building, in course of erection.
Still more lofty edifices have been going skyward in other places.
Already in New York there are a great number of lofty piles due to the
introduction of the lifts or elevators, by which an office on the tenth floor
is made as convenient as one on the second. These buildings usually
receive the name of the owners of the structure, who occupy, perhaps,
only one floor. To mention only a few. There is the American Tract
Society building, with its twenty-three stories, 285 feet high, which is
one of the latest and handsomest of these tall piles in the city. See
Plate IV. Still loftier is the St. Paul building, fronting the New York Post-Office
at the junction of Park Row and Broadway. This structure is
splayed at the angle between Ann Street and Broadway, where its width
is 39½ feet, while its loftiest part has frontages of about 30 feet along
each of these thoroughfares. The height is no less than 313 feet above
the pavement, and the number of stories is twenty-five. This building is
faced with light yellow limestone, and although it was commenced only
in the summer of 1895, it was expected to be ready for occupation by the
autumn of 1896. Even this great height is overtopped by the Manhattan
Life Insurance Company’s building, rising 330 feet, and remarkable as
perhaps beyond previous record of quickness in building a gigantic
structure. Obviously, the foundations of such a building must be most
seriously considered, prepared and tested, before the great bulk of the
building is begun, and in the New York Engineering Magazine one of
the architects has given a full account, with complete illustrations, of all
the works, from the rock foundation to the completed edifice. A description
of the foundation work, though most interesting for the professional
engineer, would probably have little attraction for the general reader;
79but its importance may be inferred from the fact of its having taken
nearly six months for its completion, while the huge superstructure required
only eight months. The eighteenth tier of beams was reached in
“three months from the time the foundations were ready on which to set
the first piece of steel, composing the bolsters that support the cantilever
system.... The substructure, which starts in bed-rock and continues
to the cellar-floor, consists of fifteen piers, varying in size from 9 feet in
diameter, to 21 feet 6 inches by 25 feet square.... The number of bricks
used in the piers amounted to 1,500,000. From this it may be seen that
a good-sized building was sunk out of sight before any part of the superstructure
could be begun.” An open court within the main structure,
special framing for the arrangements of the company’s offices on the sixth
floor, the great height and weight of the tower, and the requisite provision
for wind-bracing, delayed in some degree a regular advance of the stories;
80but within three months no less than 5,800 tons were placed in position.
There were girders weighing 40 tons, many columns of 10 and 12 tons,
and cantilevers of 80 tons weight and 67 feet long. Strange to say, that
in a building of this magnitude, where such masses had to be raised 300
feet into the air, there was not a single accident involving loss of life.
When four stories of the steel framework had been put up, the bricklayers
were set to work, and they followed the frame-setters throughout. After
the masons came the pipe-layers, with their ten miles of pipes, followed
by electricians, fixing their thirty-five miles of communicating wires.
Thirty thousand cubic feet of stone was cut and set on the Broadway front
in eighty days. Then craftsmen of the different trades followed each other,
or worked in harmony together, story after story upwards: the engineers
for boilers, heating, and elevators, the plumbers, the decorators, the
carpenters and cabinet-makers, the plasterers, the marble and tile workers,
81the gasmen, etc. In fine, every story was completely finished and ready
for occupation in eight months after the start from the foundations.
The shortness of the time in which these lofty buildings were run up is
not less remarkable than the completeness of their fittings, which comprise
everything requisite for communication within the premises and in
connection with the outer world. The elevators or lifts are the perfection
of mechanism in their way, and act with wonderful smoothness and
regularity; of these are usually two at least, as well as an ample staircase.
Notwithstanding all these appliances, some disastrous and fatal conflagrations
have occurred at buildings erected on the “tall” principle; and as
“business premises” of even 380 feet high are projected, the authorities
have been considering the desirability of restricting the heights. It has
been proposed that offices should not exceed in height 200 feet; hotels,
150 feet; and private houses, 75 feet.
The Paris example of an engineering feat upon an unprecedented
scale having proved sufficiently captivating for the general public to
ensure for itself a great commercial success, even amid the attractions of
an International Exhibition, was not lost upon the enterprising people of
the States when the “World’s Fair” at Chicago was in preparation in
1893. It was then that Mr. G. W. G. Ferris, the head of a firm of
bridge constructors at Pittsburg, conceived the idea of applying his
engineering skill to the erection of a huge wheel, revolving in a vertical
plane, with cars for persons to sit in, constituting, in fact, an enormous
“merry-go-round,” as the machine once so common at country fairs was
called. The novelty of the Chicago erection was, therefore, not the
general idea, but the magnitude of the scale, which, for that reason, involved
the application of the highest engineering skill, and the solution of
hitherto unattempted practical problems. Several thousand pounds were,
in fact, expended on merely preliminary plans and designs. The great
wheel at Chicago was 250 feet in diameter, and to its periphery were
hung thirty-six carriages, each seating forty persons. At each revolution,
therefore, 1,440 people would be raised in the air to the height of 250 feet,
and from that elevation afforded a splendid prospect, besides an experience
of the peculiar sensation like that of being in a balloon, when the
spectator has no perception of his own motion, but the objects beneath
appear to have the contrary movement, that is to say, they seem to be
sinking when he is rising, and vice versâ. The axle of the Chicago wheel
was a solid cylinder, 32 inches in diameter and 45 feet long; on this were
two hubs, 16 feet in diameter, to which were attached spoke rods, 2½ inches
in diameter, passing in pairs to an inner crown, which was concentric
with the outer rim, but 40 feet within it. The inner and outer crowns
were connected together, and the former joined to the crown of the twin
wheel by an elaborate system of trusses and ties, which, however, left an
open space between the rims of 20 feet from the outside. These last were
formed of curved riveted hollow beams, in section 25½ inches by 19
inches, and between them, slung upon iron axles through the roofs, were
suspended, at equal intervals, the thirty-six carriages, each 27 feet long,
and weighing 13 tons without its passengers, who added 3 tons more to
the weight. The wheel with its passengers was calculated to weigh about
831,200 tons, and it rested on two pyramidal skeleton towers of ironwork
140 feet high, having bases 50 feet by 60 feet. The wheel was moved by
power applied at the lowest point, the peripheries of both the rims having
great cogs 6 inches deep and 18 inches apart, which engaged a pair of
large cog-wheels, carried on a shaft 12 inches in diameter.
Fig. 26g.—Original Design for the Great Wheel.
This curious structure was not begun until March, 1893, yet it was set
in motion three months afterwards, having cost about £62,500. The
Company had to hand over to the Exhibition one half of the receipts after
the big wheel had paid for its construction, but even then they realised
a handsome profit, and at the close of the World’s Fair, they sold the
machine for four-thirds of its cost, in order that it might be re-erected at
Coney Island.
No sooner had the great Ferris wheel at Chicago proved a financial
success than an American gentleman, Lieutenant Graydon, secured a
patent for a like machine in the United Kingdom; and as it has now become
almost a matter of course that some iron or steel structure, surpassing
everything before attempted, should form a part of each great
exhibition, a Company was at once formed in London, under the title of
“The Gigantic Wheel and Recreation Towers Co., Limited,” to construct
and work at the Earl’s Court Oriental Exhibition of 1895, a great
wheel, similar in general form to that of Chicago. But the design of the
London wheel had some new features, as will be seen from the sketches,
Fig. 26c (from The Engineer of 20th April, 1894), and, moreover, having
been planned of larger dimensions than its American prototype, presented
additional engineering problems of no small complexity. After due
deliberation the scheme of the work was entrusted to Mr. Walter B.
Basset, a talented young engineer, connected with the firm of Messrs.
Maudslay, Sons, & Field, and already experienced in designing iron
structures. Under this gentleman, with the assistance of Mr. J. J.
Webster in carrying out some of the details, the work has been so successfully
accomplished that the “Great Wheel” of 1895 may be cited as
one of the crowning mechanical triumphs of the nineteenth century. The
original design has not been followed so far as regards the lower platforms
for refreshment rooms, &c. Plate V., for which we are indebted
to Mr. Basset, is a photographic representation of the actual structure.
The wheel at Earl’s Court exceeds the Ferris wheel in diameter by 50
feet, being 300 feet across. It is supported on two towers, 175 feet high,
each formed by four columns 4 feet square, built of steel plates with internal
diaphragms, and surmounted by balconies that may be ascended in
elevators raised by a weight of water, which, after having been discharged
into a reservoir under the ground level, is again pumped up to the top
of the towers. Between the balconies on each tower there is also a
communication through the axle of the wheel, which, instead of being
solid as at Chicago, is a tube of 7 feet diameter, and 35 feet long, made
in sections, riveted together, of steel 1 inch thick, and weighing no
less than 58 tons. The raising and fixing in its high place of such a mass
of metal required specially ingenious devices, which have been greatly
appreciated by professional engineers. But for these devices, the erection
of scaffolding in the ordinary way of proceeding would have entailed an
outlay simply enormous. The axle is stiffened by projecting rings, and,
between pairs of these, the spoke rods are attached by pins 3 inches in
diameter. The axle was the production of Messrs. Maudslay, Field &
Co.; all the rest of the metal work was made at the Arrol Works at
84Glasgow, and the carriages were constructed by Brown, Marshall & Co.,
of Birmingham. The Earl’s Court wheel is turned by a mechanism different
from that of the Chicago wheel, for whereas the latter was provided
with cogs, the former has two chains, each 1,000 feet long and 8 tons
weight, surrounding the periphery of the wheel on either side. The
chains go over drums in the engine-shed, from which they pass underground
to guide-pulleys, and as they unwind from the Great Wheel,
they again go over guide-pulleys to lead them back to the drums.
These chains are firmly held throughout in the jaws of V-shaped grooves,
and there are arrangements for taking up the slack. The drums are
actuated by wheel gearing, connected with two horizontal Robey steam
engines, each of 50 horse-power, one on either side, capable of being
worked singly or together. It is, however, found sufficient to use the
engine of one side only, and even then to work it at but 16 horse-power,
and the operation can be controlled by one man, who has also
the command of a brake. Both starting and stopping are accomplished
with the greatest smoothness and absence of strain or jar. There are
forty carriages, each 25 feet long, 9 feet wide, and 10 feet high. Each
will accommodate forty passengers, and these enter at the ends from
eight platforms at different heights from the ground, so arranged as to be
on the level of the eight lowest carriages while the wheel is stationary.
The passengers who have had their ride leave at the other end of the
carriages by eight similar platforms on the other side of the wheel. After
the change of passengers in one set of eight carriages, the wheel is turned
through exactly one-fifth of a revolution, which has the effect of bringing
the next eight carriages to the level of the platforms, and it is again
brought to a standstill whilst the change of passengers is taking place;
and so on, until the whole freight of say 1,600 persons has been changed
during the five stoppages in one revolution, for which about thirty-five
minutes are required, and the process of emptying and filling eight
carriages at once is repeated. There are first and second class carriages,
the charge for the former being two shillings, and for the latter one
shilling; so that, reckoning 800 passengers of each class, one turn would
bring to the treasury the handsome sum of £120.
The sensations experienced in a journey on the Great Wheel are, as
already mentioned, comparable to those enjoyed by the aërial voyagers in
a balloon, where all perception of proper motion is lost, and it is the
world beneath that seems to recede and float away, presenting the while
a strangely changing panorama. Many people who have never made a
balloon ascent yet know the calm delight of floating in a boat without
effort down some placid stream, unconscious of any motion beyond that
vaguely inferred from the silent apparent gliding by of the banks. Very
similar are, in part, the feelings of the passenger who is almost imperceptibly
carried up into the air in a carriage of the Great Wheel, but the
vertical direction of the movement, and the gradual expansion of the
horizon as the vertex is approached, lend an unwonted novelty to the
situation. From the Earl’s Court Wheel the view is both interesting and
extensive, for on a clear day the prospect stretches as far as the Royal
Castle of Windsor.
The “Gigantic Wheel” at Earl’s Court was inaugurated on the 11th
July, 1895, in the presence of an assemblage of 5,000 people, including
many distinguished personages, who were all treated to a ride. Plate
I. shows a portion of the wheel and carriages as in motion.
PLATE V.
GENERAL VIEW OF THE GREAT WHEEL AT EARL’S COURT.
85
Fig. 27.—Sir Joseph Whitworth.
TOOLS. — THE BLANCHARD LATHE. — SAWING MACHINES.
Of the immense variety of tools and mechanical contrivances employed
in modern times, by far the greatest number are designed to impart
to certain materials some definite shape. The brickmaker’s mould, the
joiner’s plane, the stonemason’s chisel, the potter’s wheel, are examples of
simple tools. More elaborate are the coining press, the machine for planing
iron, the drilling machine, the turning lathe, the rolling mill, the Jacquard
loom. But all such tools and machines have one principle in common—a
principle which casual observers may easily overlook, but one which is of
the highest importance, as its application constitutes the very essence of
the modern process of manufacture as distinguished from the slow and
laborious mode of making things by hand. The principle will be easily
understood by a single example. Let it be required to draw straight lines
across a sheet of paper. Few persons can take a pen or pencil, and do
this with even an approach to accuracy, and at best they can do it but
slowly and imperfectly. But with the aid of a ruler any number of straight
lines may be drawn rapidly and surely. The former case is an instance of
making by hand, the latter represents manufacturing, the ruler being the
tool or machine. Let it be observed that the ruler has in itself the kind
of form required—that is to say, straightness—and that in using it we copy
or transfer this straightness to the mark made on the paper. This is a
86simple example of the copying principle, which is so widely applied in
machines for manufacturing; for, in all of these, materials are shaped or
moulded by various contrivances, so as to reproduce certain definite forms,
which are in some way contained within the machine itself. This will be
distinctly seen in the tools which are about to be described.
Fig. 28.—Whitworth’s Screw Dies and Tap.
Probably no one mechanical contrivance is so much and so variously
applied as the Screw. The common screw-nail, which is so often used by
carpenters for fastening pieces of metal on wood, or one piece of wood to
another, is a specimen of the screw with which everybody is familiar. The
projection which winds spirally round the nail is termed the thread of the
screw, and the distance that the thread advances parallel to the axis in
one turn is called the pitch. It is obvious that for each turn the screw
makes it is advanced into the wood a depth equal to the pitch, and that
there is formed in the wood a hollow screw with corresponding grooves
and projections. Screws are formed on the ends of the bolts, by which
various parts are fastened together, and the hollow screws which turn on
the ends of the bolts are termed nuts. The screws on bolts and nuts, and
other parts of machines, were formerly made with so many different pitches
that, when a machine constructed by one maker had to be repaired by
another, great inconvenience was found, on account of the want of uniformity
in the shape and pitch of the threads. A uniform system was many
years ago proposed by Sir Joseph Whitworth, and adopted by the majority
of mechanical engineers, who agreed to use only a certain defined series of
pitches. The same engineer also contrived a hand tool for cutting screws
with greater accuracy than had formerly been attained in that process.
A mechanic often finds it necessary to form a screw-thread on a bolt, and
also to produce in metal a hollow screw. The reader may have observed
gas-fitters and other workmen performing the first operation by an instrument
having the same general appearance as Fig. 28. This contains
hard steel dies, which are made to press on the bolt or pipe, so that when
the guide-stock is turned by the handles, the required grooves are cut out.
87The arrangement of these dies in Sir Joseph Whitworth’s instrument is
shown in Fig. 28, which represents the central part of the guide-stock;
A, B, C are the steel dies retained in their places, when the instrument is in
use, by a plate which can be removed when it is necessary to replace one
set of dies by another, according to the pitch of thread required. The
figure also shows the set of dies, A, B, C, removed from the guide-stock. D is
the work, pressed up against the fixed die, A, by B and C, the pressure being
applied to these last as required by turning the nut, thus drawing up the key,
E, so that the inclined planes, f, g, press against similar surfaces forming
the ends of the dies. For producing the hollow screws, taps are provided,
which are merely well-formed screws, made of hard steel and having the
threads cut into detached pieces by several longitudinal grooves, as represented
in the lower part of Fig. 28.
Fig. 29.—Screw-cutting Lathe.
The method of forming screws by dies and taps is, however, applicable
only to those of small dimensions, and even for these it is not employed
where great accuracy is required. Perfect screws can only be cut with a
lathe, such as that represented in Fig. 29. In this we must first call the
reader’s attention to the portion of the apparatus marked A, which receives
the name of the slide-rest. The invention of this contrivance by Maudsley
had the effect of almost revolutionizing mechanical art, for by its aid it
became possible to produce true surfaces in the lathe. Before the slide-rest
was introduced, the instrument which cut the wood or metal was held in
the workman’s hand, and whatever might be his skill and strength, the
steadiness and precision thus obtainable were far inferior to those which
could be reached by the grip of an iron hand, guided by unswerving bars.
The slide-rest was contrived by Maudsley in the first instance for cutting
screws, but its principle has been applied for other purposes. This
principle consists in attaching the cutting tool to a slide which is incapable
of any motion, except in the one direction required. Thus the slide, A,
represented in Fig. 29, moves along the bed of the lathe, B, carrying the
cutter with perfect steadiness in a straight line parallel to the axis of the
lathe. There are also two other slides for adjusting the position of the
cutter; the handle, a, turns a screw, which imparts a transverse motion to
the piece, b, and the tool receives another longitudinal movement from the
88handle, c. The pieces are so arranged that these movements take place in
straight lines in precisely the required direction, and without permitting
the tool to be unsteady, or capable of any rocking motion. In Whitworth’s
lathe, between the two sides of the bed, and therefore not visible in the figure,
is a shaft placed perfectly parallel to the axis of the lathe. One end of this
shaft is seen carrying the wheel, C, which is connected with a train of wheels,
D, and is thus made to revolve at a speed which can be made to bear any
required proportion to that of the mandril, E, of the lathe, by properly
arranging the numbers of the teeth in the wheels; and the machine is
provided with several sets of wheels, which can be substituted for each
other. The greater part of the length of this shaft is formed with great
care into an exceedingly accurate screw, which works in a nut forming
part of the slide-rest. The effect, therefore, of the rotation of the screw
is to cause the slide-rest to travel along the bed of the lathe, advancing
with each revolution of the screw through a space equal to its pitch distance.
There is an arrangement for releasing the nut from the guiding-screw,
by moving a lever, and then by turning the winch the slide-rest
is moved along by a wheel engaging the teeth of a rack at the back of
the lathe. Now, if the train of wheels, C D, be so arranged that the screw
makes one revolution for each turn of the mandril, it follows that the cutting
tool will move longitudinally a distance equal to the pitch of the
guiding-screw while the bar placed in the lathe makes one turn. Thus
the point of the cutter will form on the bar a screw having the same pitch
as the guiding-screw of the lathe.
Here we have a striking illustration of the copying principle, for the
lathe thus produces an exact copy of the screw which it contains. The
screw-thread is traced out on the cylindrical bar, which is operated upon by
the combination of the circular motion of the mandril with the longitudinal
movement of the slide-rest. By modifying the relative amounts of these
movements, screw-threads of any desired pitch can be made, and it is for
this purpose that the change wheels are provided. If the thread of the
guiding-screw makes two turns in one inch, one revolution of the wheel C
will advance the cutter half an inch along the length of the bar. If the
numbers of teeth in the wheels be such that the wheel D makes ten revolutions
while C is making one, then in the length of half an inch the thread
of the screw produced by the cutter will go round the core ten times, or,
in technical language, the screw will be of 1 20 inch pitch.
Fig. 30.—Whitworth’s Measuring Machine.
Since a screw turning in a nut advances only its pitch distance at each
revolution, a finely-cut screw furnishes an instrument well adapted to impart
a slow motion, or to measure minute spaces. Suppose a screw is cut
so as to have fifty threads in an inch, then each turn will advance it 1 50 in.;
half a turn 1 100 in.; a quarter of a turn, 1 200, and so on. It is quite easy to
attach a graduated circle to the head of the screw, so that, by a fixed
pointer at the circumference, any required fraction of a revolution may be
read off. Thus if the circle had two hundred equal parts, we could, by
turning the screw so that one division passed the index, cause the screw
to advance through 1 200 of 1 50 inch, or 1 10000 part of an inch. This is the
method adopted for moving the cross-wires of the instruments for measuring
very small spaces under the microscope. Sir Joseph Whitworth, who has
done so many great things in mechanical art, was the first mechanician to
perceive the importance of extreme accuracy of workmanship, and he
invented many beautiful instruments and processes by which this accuracy
might be attained. Fig. 30 represents one of his measuring machines,
89intended for practical use in the workshop, to test the dimensions of pieces
of metal where great precision is required. The base of the machine is
constructed of a rigid cast iron bed bearing a fixed headstock, A, and a
movable one, B, the latter sliding along the bed, C, with a slow movement,
when the handle, D, is turned. This slow motion is produced by a screw
on the axis, a, working in the lower part of the headstock, just as the slide-rest
is moved along the bed of the lathe. The movable headstock, when
it has been moved into the position required, is firmly clamped by a thumbscrew.
The face of the bed is graduated into inches and their subdivisions.
Here it should be explained that the machine is not intended to be used
for ascertaining the absolute dimensions of objects, but for showing by what
fraction of an inch the size of the work measured differs from a certain
standard piece. Each headstock carries a screw of 1 20 inch pitch, made
with the greatest possible care and accuracy. To the head of the screw
in the movable headstock is attached the wheel, b, having its circumference
divided into 250 equal parts, and a fixed index, c, from which its graduations
may be counted. An exactly similar arrangement is presented in connection
with the screw turning in the fixed headstock, but the wheel is much larger,
and its circumference is divided in 500 equal parts. It follows, therefore,
that if the large wheel be turned so that one division passes the index, the
bar moves in a straight line 1 500 of the 1 20 of an inch, that is, 1 10000 an inch.
The ends of the bars, d and e, are formed with perfectly plane and parallel
surfaces, and an ingenious method is adopted of securing equality of pressure
when comparisons are made. A plate of steel, with perfectly parallel faces,
called a gravity-piece, or feeler, is placed between the flat end of the bar and
the standard-piece, and the pressure when the screw-reading is taken must
be just sufficient to prevent this piece of steel from slipping down, and
that is the case when the steel remains suspended and can nevertheless be
easily made to slide about by a touch of the finger. Thus any piece which,
90with the same screw-readings, sustains the gravity-piece in the same manner
as the standard, will be of exactly the same length; or the number of divisions
through which the large wheel must be turned to enable it to do so
tells the difference of the dimensions in ten-thousandth parts of an inch. By
this instrument, therefore, gauges, patterns, &c., can be verified with the
greatest precision, and pieces can be reproduced perfectly agreeing in their
dimensions with a standard piece. Thus, for example, the diameters of
shafting can be brought with the greatest precision to the exact size required
to best fit their bearings.
In another measuring machine on the same principle the delicacy of the
measurement has been carried still farther, by substituting for the large
divided wheel one having 200 teeth, which engage an endless screw or
worm. This will easily be understood by reference to Fig. 31, where a similar
arrangement is applied to another purpose. Imagine that a wheel like P,
Fig. 31, but with 200 teeth, has taken the place of E in Fig. 30, and that the
wheel, T, on the axis of the endless screw is shaped like E, Fig. 30. One
turn of the axis carrying the endless screw, therefore, turns the wheel
through 1 200 of a revolution, and as this axis bears a graduated head, having
250 divisions, the screw having 20 threads to the inch, is, when one division
passes the index, advanced through a space equal to 1 250 × 1 200 × 1 20, or
1 1000000 an inch; that is, the one-millionth part of an inch. This is an
interval so small that ten times its length would hardly be appreciated with
the highest powers of the microscope, and the machine is far too delicate
for any practical requirements of the present day. It will indicate the
expansion caused by heat in an iron bar which has merely been touched
with the finger for an instant, and even the difference of length produced
by the heat radiated from the person using it. A movement of 1 1000000 of
an inch is shown by the gravity-piece remaining suspended instead of falling,
and the piece falls again when the tangent-screw is turned back
through 1 250 of a revolution, a difference of reading representing a possible
movement of the measuring surface through only 2 1000000 an inch. This
proves the marvellous perfection of the workmanship, for it shows that the
amount of play in the bearings of the screws does not exceed one-millionth
of an inch.
A good example of a machine-tool is the Drilling Machine, which is used
for drilling holes in metal. Such a machine is represented in Fig. 31, where
A is the strong framing, which is cast in a single piece, in order to render
it as rigid as possible. The power is applied by means of a strap round
the speed pulley, B, by which a regulated speed is communicated to the bevel
wheel, C, which drives D, and thus causes the rotation of the hollow shaft,
E. In the lower part of the latter is the spindle which carries the drilling
tool, F, and upon this spindle is a longitudinal groove, into which fits a
projection on the inside of E. The spindle is thus forced to rotate, and is at
the same time capable of moving up and down. The top of the spindle
is attached to the lower end of the rack, G, by a joint which allows the
spindle to rotate freely without being followed in its rotation by the rack,
although the latter communicates all its vertical movements to the spindle,
as if the two formed one piece. The teeth of the rack are engaged by
a pinion, which carries on its axis the wheel H, turned by an endless screw
on the shaft, I, which derives its motion by means of another wheel and
endless screw from the shaft, K. The latter is driven by a strap passing
over the speed pulleys, L and M, and thus the speed of the shaft K can
be modified as required by passing the strap from one pair of pulleys to
91another. The result is that the rack is depressed by a slow movement,
which advances the drill in the work, or, as it is technically termed, gives
the feed to the drill. By a simple piece of mechanism at N the connection
of the shafts K and I can be broken, and the handle O made to communicate
a more rapid movement to I, so as to raise up the drill in a position to
begin its work again, or to bring it quickly down to the work, and then the
arrangement for the self-acting feed is again brought into play. By turning
the wheel, P, the table, Q, on which the work is fastened, is capable of being
raised or lowered, by means of a rack within the piece R, acted on by a
pinion carried on the axle, P. The table also admits of a horizontal motion
by the slide S, and may besides be swung round when required.
Fig. 31.—Whitworth’s Drilling Machine.
The visitor to an engineer’s workshop cannot fail to be struck with the
92operation of the powerful Lathes and Planing Machines, by which long thick
flakes or shavings of iron are removed from pieces of metal with the same
apparent ease as if the machine were paring cheese. The figure on the
opposite page represents one of the larger forms of the planing machine,
as constructed by Sir J. Whitworth. The piece of work to be planed is
firmly bolted down to the table, A, which moves upon the Ꮩ-shaped surfaces,
running its whole length, and accurately fitting into corresponding grooves
in a massive cast iron bed. The bevel wheel, of which a portion is seen at
B, is keyed on a screw, which extends longitudinally from end to end of
the bed. This screw works in nuts forming part of the table, and as it
turns in sockets at the ends of the bed, it does not itself move forward, but
imparts a progressive movement to the table, and therefore to the piece of
metal to be planed. As this table must move backwards and forwards,
there must be some contrivance for reversing the direction of the screw’s
rotation, and this is accomplished in a beautifully simple manner by an
arrangement which a little consideration will enable any one to understand.
It will be observed that there are three drum-pulleys at C. Let the reader
confine, for the present, his attention to the nearest one, and picture to himself
that the shaft to which it is attached is placed in the same horizontal
plane as the axis of the screw and at right angles to it, passing in front of
bevel wheel B. A small bevel wheel turning with this shaft, and engaging
the teeth of the wheel B, may, it is plain, communicate motion to the screw.
Now let the reader consider what will be the effect on the direction of the
rotation of B of applying the bevelled pinion to the nearer or to the farther
part of its circumference, supposing the direction of the rotation of this
pinion to be always the same. He will perceive that the direction in one
case will be the reverse of that in the other. The shaft to which the nearest
pulley is attached carries a pinion engaging the wheel at its farther edge,
and therefore the rotation of this pulley in the same direction as the hands
of a watch causes the wheel B to rotate so that its upper part moves towards
the spectator. The farthest pulley, a, turns with a hollow shaft, through
which the shaft of the nearest pulley simply passes, without any connection
between them, and this hollow shaft carries a pinion, which engages the
teeth of B at the nearer edge, and, in consequence, the rotation of the
farther pulley, a, in the direction of the hands of a watch, would cause the
upper part of B to be moving from the spectator. The middle pulley, b,
runs loosely on the shaft, and the driving-strap passes through the guide,
c, and it is only necessary to move this, so as to shift the strap from one
drum to another, in order to reverse the direction of the screw and the
motion. This shifting of the strap is done by a movement derived from
the table itself, on which are two adjustable stops, D and E, acting on an
arrangement at the base of the upright frame when they are brought up to
it by the movement of the table, so as not only to shift the strap, but also
to impart a certain amount of rotation to upright shaft, F, in each direction
alternately. The piece which carries the tools, G and H, is placed horizontally,
and can be moved vertically by turning the axis, I, thus causing an
equal rotation of two upright screws of equal pitch, which are contained
within the uprights and work in nuts, forming part of the tool-box. The
pieces carrying the tools are moved horizontally by the screws which are
seen to pass along the tool-box, and these screws receive a certain regulated
amount of motion at each reversal of the movement of the table from
the mechanism shown at K. The band-pulley, L, receives a certain amount
of rotation from the same shaft, and the catgut band passing round the tops
94of the cylinders which carry the cutters is drawn in alternate directions at
the end of each stroke, the effect being to turn the cutters half round, so
as always to present their cutting edges to the work. There are also contrivances
for maintaining the requisite steadiness in the tools and for
adjusting the depth of the cut. The cutting edge of the tools is usually of
a Ꮩ-shape, with the angle slightly rounded, and the result of the process
is not the production of a plane, but a grooved surface. But by diminishing
the amount of horizontal feed given to the cutters, the grooves may be
made finer and finer, until at length they disappear, and the surface is
practically a plane. Planing machines are sometimes of a very large size.
Sir J. Whitworth has one the table of which is 50 ft. in length, and the
machine is capable of making a straight cut 40 ft. long in any article not
exceeding 10 ft. 6 in. high or 10 ft. wide.
Fig. 32.—Whitworth’s Planing Machine.
Fig. 33.—Pair of Whitworth’s Planes, or Surface Plates.
The copying principle is evident in this machine; for the plane surface
results from the combination of the straightness of the bed with the straightness
of the transverse slide along which the tools are moved. It should, moreover,
be observed that it is precisely this machine which would be employed
for preparing the straight sliding surfaces required in the construction of
planing and other machines, and thus one of these engines becomes the
parent, as it were, of many others having the same family likeness, and so
on ad infinitum. Thus, having once obtained perfectly true surfaces, we
can easily reproduce similar surfaces. But the reader may wish to know
how such forms have been obtained in the first instance; how, for example,
could a perfectly plane surface be fashioned without any standard for comparison?
This was first perfectly done by Sir J. Whitworth, forty-five
years ago. Three pieces of iron have each a face wrought into comparatively
plane surfaces; they are compared together, and the parts which are prominent
are reduced first by filing, but afterwards, as the process approaches
completion, by scraping, until the three perfectly coincide. The parts where
the plates come in contact with each other are ascertained by smearing one
of them with a little oil coloured with red ochre: when another is pressed
against it, the surfaces of contact are shown by the transference of the
red colour. Three plates are required, for it is possible for the prominences
of No. 1 exactly to fit into the hollows of No. 2, but in that case both could
not possibly exactly coincide with the surface of No. 3; for if one of them
did (say No. 1), then No. 3 must be exactly similar to No. 2, and consequently
when No. 2 was applied to No. 3, hollow would be opposed to
95hollow and prominence to prominence. A little reflection will show that
only when the three surfaces are truly plane will they exactly and entirely
coincide with each other. The planes, when thus carefully prepared, approach
to the perfection of the ideal mathematical form, and they are used
in the workshop for testing the correctness of surfaces, by observing the
uniformity or otherwise of the impression they give to the surface when
brought into contact with it, after being covered by a very thin layer of oil
coloured by finely-ground red ochre.
Fig. 33 represents a small pair of Whitworth’s planes. When one of
these is placed horizontally upon the other, it does not appear to actually
come in contact with it, for the surfaces are so true that the air does not
easily escape, but a thin film supports the upper plate, which glides upon
it with remarkable readiness (A). When, however, one plate is made to
slide over the other, so as to exclude the air, they may both be lifted by
raising the upper one (B). This effect has, by several philosophers, been
attributed to the mere pressure of the atmosphere; but recent experiments
of Professor Tyndall’s show that the plates adhere even in a vacuum. The
adhesion appears therefore to be due to some force acting between the
substances of the plates, and perhaps identical in kind with that which
binds together the particles of the iron itself.
Fig. 34.—Interior of Engineer’s Workshop.
96
Fig. 35.—The Blanchard Lathe.
This machine affords a striking example of the application of the copying
principle which is the fundamental feature of modern manufacturing
processes. It would hardly be supposed possible, until the method
had been explained, that articles in shape so unlike geometrical forms as
gun-stocks, shoemakers’ lasts, &c., could be turned in a lathe. The mode
in which this is accomplished is, however, very simple in idea, though in
carrying that idea into practice much ingenious contrivance was required.
The illustration, Fig. 35, represents a Blanchard’s lathe, very elegantly constructed
by Messrs. Greenwood and Batley, of Leeds. The first obvious
difference between an ordinary lathe and Blanchard’s invention is that in
the former the work revolves rapidly and the cutting-tool is stationary, or
only slowly shifts its position in order to act on fresh portions of the work,
while in the latter the work is slowly rotated and the cutting-tools are made to
revolve with very great velocity. Again, it will be observed that the headstock
of the Blanchard lathe, instead of one, bears two mandrels, having
their axes parallel to each other. One of these carries the pattern, C, which
in the figure has the exact shape of a gun-stock that is to be cut in the piece
of wood mounted on the nearer spindle. One essential condition in the
arrangement of the apparatus is that the pattern and the work having been
fixed in similar and parallel positions, shall always continue so at every point
of their revolutions. This is easily accomplished by placing exactly similar
toothed wheels on the two axles, and causing these to be turned by one and
the same smaller toothed wheel or pinion. The two axles must thus always
turn round in the same direction and with exactly the same speed, so that the
work which is attached to one, and the pattern which is fixed on the other,
will always be in the same phase of their revolutions. If, for example, the
part of the wood which is to form the upper part of the gun-stock is at the
97bottom, the corresponding part of the pattern will also be at the bottom,
as in the figure, and both will turn round together, so that every part of
each will be at every instant in a precisely similar position. The wood to
be operated upon is, it must be understood, roughly shaped before it is put
into the lathe. The toothed wheels and the pinion which drives them are
in the figure hid from view by the casing, h, which covers them. The
pinion receives the power from a strap passing over f. The cutters are
shown at e; they are placed radially, like the spokes of a wheel, and have
all their cutting edges at precisely one certain distance from the axis on
which they revolve, so that they all travel through the same circle. These
cutting-edges, it may be observed, are very narrow, almost pointed. The
shaft carrying the cutters is driven at a very high speed, by means of a
strap passing over k and i. The number of revolutions made by the cutters
in one second is usually more than thirty. The great peculiarity of the
lathe consists in the manner in which the position of the cutters is made to
vary. The axle which carries them rotates in a kind of frame, which
can move backwards and forwards, so that the cutters may be readily put
at any desired distance from the axis of the work. Their position is, however,
always dependent on the pattern, for, fixed in a similar frame, b, which
is connected with the former, is a small disc wheel, a, having precisely the
same radius as that of the circle traced out by the cutters, and this disc is
made by a strong spring to press against the pattern. The cutters, being
fixed in the same rocking-frame which carries this guiding-wheel, must
partake of all its backward and forward motions, and as the cutting-wheel
and the guide-wheel are so arranged as to have always the same relative
positions to the axes of the two headstocks, it follows that the edges of the
cutters will trace out identically the same form as the circumference of the
guiding-disc. The latter is, of course, not driven round, but simply turns
slowly with the pattern by friction, for it is pressed firmly against the pattern
by a spring or weight acting on the frame, in order that the cutters may be
steadily maintained in their true, but ever-varying, position. The rocking-frame
receives a slow longitudinal motion by means of the screw, n, so that
the cutters are carried along the work, and the guide along the pattern.
The whole arrangement is self-acting, so that when once the pattern and
the rough block of wood have been fixed in their positions, the machine
completes the work, and produces an exact repetition of the shape of the
pattern. It is plain that any kind of forms can be easily cut by this lathe,
the only condition being that the surface of the pattern must not present
any re-entering portions which the edge of the guide-wheel cannot follow.
The machine is largely used for the purposes named above, and also for
the manufacture of the spokes of carriage-wheels. The limits of this article
will not permit of a description of the beautiful adjustments given to the
mechanism in the example before us, particularly in the arrangement for
driving the cutters in a framework combining lateral and longitudinal
motions; but the intelligent reader may gather some hints of these by a
careful inspection of the figure. The machine is sometimes made with
the frame carrying the guide-wheel and cutters, not rocking but sliding in
a direction transverse to the axes of the headstocks. It is extremely interesting
to see the Blanchard lathe at work, and observe how perfectly and
rapidly the curves and form of the patterns seem to grow, as it were, out
of the rudely-shaped piece of wood, which, of course, contains a large excess
of material, or, in the picturesque and expressive phrase of the workmen,
always gives the machine something to eat.
98
Fig. 36.—Vertical Saw.
With the exception of the last, all the machines hitherto described in
the present article are distinguished by this—they are tools which
are used to produce other machines of every kind. Without such implements
it would be impossible to fashion the machines which are made to
serve so many different ends. Another peculiarity of these tools has also
been referred to, namely, that they are especially serviceable, and indeed
essential, for the reproduction of others of the same class. Thus, the accurate
leading-screw of the lathe is the means used to cut other accurate
screws, which shall in their turn become the leading-screws of other lathes,
and a lathe which forms a truly circular figure is a necessary implement for
the construction of another lathe which shall also produce truly circular
figures. In these tools, therefore, we find the copying principle, to which
allusion has been already made, as the great feature of all machines; but
in order to bring this principle still more clearly before the reader, we have
described in the Blanchard Lathe a machine of a somewhat different class,
because it embodied a very striking illustration of the principle in question.
We are far from having described all the implements of the mechanical
engineer, or even all the more interesting ones; for example, we have given
no account of the powerful lathes in which great masses of iron are turned,
or of the analogous machines, which, with so much accuracy, shape the
internal surfaces of the cylinders of steam engines, of cannons, &c. The
99history of the steam engine tells us of the difficulties which Watt had to
contend with in the construction of his cylinders, for no machine at that
time existed capable of boring them with an approach to the precision which
is now obtained.
Fig. 37.—Circular Saw.
The kind of general interest which attaches to the tools we have already
described is not wanting in yet another class of machine-tools, namely,
those employed in converting timber into the forms required to adapt it
for the uses to which it is so extensively applied. And for popular illustration,
this class of tools presents the special advantage of being readily
understood as regards their purpose and mode of action, while their simplicity
in these respects does not prevent them from showing the advantages
of machine over hand labour. Everybody is familiar with the up-and-down
movement of a common saw, and in the machine for sawing
balks of timber into planks, represented in Fig. 36, this reciprocating motion
is retained, but there are a number of saws fixed parallel to each other
in a strong frame, at a distance corresponding to the thickness of the
planks. The saws are not placed with their cutting edges quite upright,
but these are a little more forward at the top, so that as they descend they
cut into the wood, but move upwards without cutting, for the teeth then
recede from the line of the previous cut, while in the meantime the balk
is pushed forward ready for the next descent of the saw-frame. This pushing
forward, or feeding, of the timber is accomplished by means of ratchet-wheels,
which are made to revolve through a certain space after each descent
of the saw-frame, and, by turning certain pinions, move forward the carriage
on which the piece of timber is firmly fixed, so that when the blades
100of the saws are beginning the next descent they are already in contact with
the edge of the former cut. To prevent the blades from moving with
injurious friction in the saw-cuts, these last are made of somewhat greater
width than the thickness of the blades, by the simple plan of bending the
teeth a little on one side and on the other alternately. The rapidity with which
the machine works, depends of course on the kind of wood operated upon,
but it is not unusual for such a machine to make more than a hundred cuts
in the minute. The figure shows the machine as deriving its motion by
means of a strap passing over a drum, from shafting driven by a steam
engine. This is the usual plan, but sometimes the steam power is applied
directly, by fixing the piston-rod of a steam cylinder to the top of the saw-frame,
and equalizing the motion by a fly-wheel on a shaft, turned by a
crank and connecting-rod.
A very effective machine for cutting pieces of wood of moderate dimensions
is the Circular Saw, represented in Fig. 37. Here there is a steel
disc, having its rim formed into teeth; and the disc is made to revolve with
very great speed, in some cases making as many as five hundred turns in
a minute, or more than eight in a second. On the bench is an adjustable
straight guide, or fence, and when this has been fixed, the workman has
only to press the piece of wood against it, and push the wood at the same
time towards the saw, which cuts it at a very rapid rate. Sometimes the
circular saw is provided with apparatus by which the machine itself pushes
the wood forwards, and the only attention required from the workman is
the fixing of the wood upon the bench, and the setting of the machine in
gear with the driving-shaft. Similar saws are used for squaring the ends
of the iron rails for railways, two circular saws being fixed upon one axle
at a distance apart equal to the length of the rails. The axle is driven at
the rate of about 900 turns per minute, and the iron rail is brought up
parallel to the axle, being mounted on a carriage, and still red hot, when
the two ends are cut at the same time by the circular saws, the lower parts
of which dip into troughs of water to keep them cool.
Fig. 38.—Pit-Saw.
101
Fig. 39.—Box Tunnel.
RAILWAYS. — THE METROPOLITAN RAILWAYS. — THE PACIFIC RAILWAY. — INCLINED RAILWAYS.
Fig. 40.—Coal-pit, Salop.
Towards the end of last century, tramways formed by laying down
narrow plates of iron, were in use at mines and collieries in several
parts of England. These plates had usually a projection or flange on the
inner edge, thus—L, in order to keep the waggons on the track, for the
wheels themselves had no flange, but were of the kind used on ordinary
roads. These flat tramways were found liable to become covered up with
dirt and gravel, so that the benefit which ought to have been obtained from
their smoothness was in a great measure lost. Edge rails were, therefore,
substituted, and the wheels were kept on the rails by having a flange cast
on the inner edge of the rim. The rails were then always made of cast
iron, for, although they were very liable to break, the great cost of making
them of wrought iron prevented that material from being used until 1820,
when the method of forming rails of malleable iron by rolling came into
use. The first time a tramway was used for the conveyance of passengers
was in 1825, when the Stockton and Darlington Railway was opened—a
length of thirty-seven miles. It appears that the carriages were at first
drawn by horses, although locomotives were used on this and other colliery
lines for dragging, at a slow rate, trains of mineral waggons. At that time
engineers were exercising their ingenuity in overcoming a difficulty which
never existed by devising plans for giving tractive power to the locomotive
through the instrumentality of rack-work rails. It never occurred to them
to first try whether the adhesion of the smooth wheel to the smooth rail
was not sufficient for the purpose. During the first quarter of the present
102century the greater part of the goods and much passenger traffic was
monopolized by the canals. It is quoted, as a proof of the careless manner
in which this service was performed, that the transport of bales of cotton
from Liverpool to Manchester sometimes occupied twice the length of time
required in their voyage across the Atlantic. When an Act of Parliament
authorizing the construction of a railway between Liverpool and Manchester
was applied for, the canal companies succeeded in retarding, by their influence,
the passing of that Act for two years. It was passed, however, in
1828, and the construction of the line was proceeded with. This line was
at first intended only for the conveyance of goods, especially of cotton and
cotton manufactures, and the waggons were to be drawn by horses. When
the line was nearly finished the idea of employing horses was, at the instigation
of Mr. George Stephenson, abandoned in favour of steam power.
The directors were divided in opinion as to whether the carriage should
be dragged by ropes wound on large drums by stationary engines, or
whether locomotives should be employed. Finally, the latter plan was
adopted, and it was also suggested that passengers might be carried. The
directors offered a prize for the best locomotive, and the result has been
already mentioned. In the light of our experience since that time, it is
curious to read of the doubts then entertained by skilful engineers about
the success of the locomotive. In a serious treatise on the subject, one
eminent authority hoped “that he might not be confounded with those
hot-brained enthusiasts who maintained the possibility of carriages being
driven by a steam engine on a railway at such a speed as twelve miles an
hour.” When the “Rocket” had accomplished the unprecedented velocity
of twenty-nine miles an hour, and the railway was opened for passengers
as well as goods, the thirty stage coaches daily plying between Liverpool
103and Manchester found their occupation gone, and all ceased to run except
one, which had to depend on the roadside towns only, while the daily number
of passengers between the two cities rose at once from 500 to 1,600. In
that delightful book, Smiles’s “Life of George Stephenson,” may be found
most interesting details of the difficulties attending the introduction of
railways, especially with regard to the construction of this first important
line. Mr. Smiles relates how the promoters of the scheme struggled against
“vested interests;” how the canal proprietors, confident at first of a secure
and continuous enjoyment of their monopoly, ridiculed the proposed railway,
and continued their exorbitant charges and tardy conveyance, pocketing
in profits the prime cost of their canal about every three years; how,
roused into active opposition, they did all in their power to thwart the new
scheme; how the Lord Derby and the Lord Sefton of that day, and other
landowners, offered every resistance to the surveyors; how the Duke of
Bridgewater’s farmers would not allow them to enter their fields, and the
Duke’s gamekeepers had orders to shoot them; how even a clergyman
threatened them with personal violence, and they had to do their work by
stealth, while the reverend gentleman was conducting the services in his
church; how newspaper and other writers declared that the locomotives
would kill the birds, prevent cows from grazing and hens from laying,
burn houses, and cause the extinction of the race of horses. All the civil
engineers scouted the idea of a locomotive railway, and Stephenson was
held up to derision as an ignoramus and a maniac by the “most eminent
lawyers,” and the most advanced and “respectable” professional C.E.s of
the time. An article appeared in the “Quarterly Review,” very favourable
to the construction of railways, but remarking in reference to a proposed
line between London and Woolwich: “What can be more palpably absurd
and ridiculous than the prospect held out of locomotives travelling twice
as fast as stage coaches! We should as soon expect the people of Woolwich
to suffer themselves to be fired off upon one of Congreve’s ricochet rockets
104as trust themselves to the mercy of a machine going at such a rate. We
will back old Father Thames against the Woolwich Railway for any sum.
We trust that Parliament will, in all railways it may sanction, limit the
speed to eight or nine miles an hour, which we entirely agree with Mr.
Sylvester is as great as can be ventured on with safety.” This passage,
which reads so strangely now, may be seen in the “Quarterly Review” for
March, 1825. But still more curious appear now the reports of the debates
in Parliament, and of the evidence taken before the Parliamentary Committee,
in which we find the opinions and fears of the best informed men
of that period, and trace the frantic efforts of the holders of the “vested
interests” to retain them, however obstructive of the public good.
Fig. 41.—Sankey Viaduct.
Fig. 42.—Rails and Cramp-gauge.
When it has been decided to construct a railway between two places,
the laying-out of the line is a subject requiring great consideration and the
highest engineering skill—for the matter is, on account of the great cost,
much more important than the setting-out of a common road. The idea
of a perfect railroad is that of a straight and level line from one terminus
to another; but there are many circumstances which prevent such an idea
from being ever carried into practice. First, it is desirable that the line
should pass through important towns situated near the route; and then
the cost of making the roadway straight and level, in spite of natural obstacles,
would be often so great, that to avoid it detours and inclines must
be submitted to—the inconvenience and the increased length of road being
balanced by the saving in the cost of construction. It is the business of
the engineer who lays out the line to take all these circumstances into consideration,
after he has made a careful survey of the country through which
the line is to pass. The cost of making railways varies, of course, very
much according to the number and extent of the tunnels, cuttings, embankments,
or other works required. The average cost of each mile of
railway in Great Britain may be stated as about £35,000. The road itself
when the rails are laid down is called the permanent way, perhaps originally
in distinction to the temporary tramways laid down by the contractors
during the progress of the works. The permanent way is formed first of
105ballast, which is a layer of gravel, stone, or other carefully chosen material,
about 2 ft. deep, spread over the roadway. Above the ballast and partly embedded
in it are placed the sleepers, which is the name given to the pieces
of timber on which the rails rest. These timbers are usually placed transversely—that
is, across the direction of the rails, in the manner shown in Fig.
42. This figure also represents the form of rails most commonly adopted,
and exhibits the mode in which they are fastened down to the sleepers by
means of the iron chairs, bc, the rail being firmly held in its place by an
oak wedge, d. These wedges are driven in while the rails are maintained
at precisely the required distance apart by the implement, e f, called a
cramp gauge, the chairs having previously been securely attached to the
sleepers by bolts or nails. The double ⟙ form of rail has several important
advantages, such as its capability of being reversed when the upper surface
is worn out, and the readiness with which the ends of the rails can be joined
by means of fish-plates. These are shown in Fig. 43, where in a we are
supposed to be looking down on the rails, and in B to be looking at them
sideways. In Fig. 44 we have the rail and fish-plates in section. The holes
in the rails through which the bolts pass are not round but oval, so that a
certain amount of play is permitted to the ends of the rails.
Fig. 43.—Fish-plate.
It may easily be seen on looking at a line of rails that they are not laid
with the ends quite touching each other, or, at least, they are not usually
in contact. The reason of this is that space must be allowed for the expansion
which takes place when a rise in the temperature occurs. If the
rails are laid down when at the greatest temperature they are likely to be
subject to, they may then be placed in actual contact; but in cold weather
a space will be left by their contraction. For this reason it is usual when
rails are laid to allow a certain interval; thus rails 20 ft. long laid when the
temperature is 70°, are placed with their ends 1 20th of an inch apart, at 30°
1 10th of an inch apart, and so on. The neglect of this precaution has sometimes
led to damage and accidents. A certain railway was opened in June,
and after an excursion train had in the morning passed over it, the midday
106heat so expanded the iron, that the rails became in some places elevated
2 ft. above the level, and the sleepers were torn up; so that, in order
to admit of the return of the train, the rails had to be hastily relaid in a
kind of zigzag. In June, 1856, a train was thrown off the metals of the
North-Eastern Railway, in consequence of the rails rising up through
expansion.
Fig. 44.—Section of Rails and Fish-plates.
The distance between the rails in Great Britain is 4 ft. 8½ in., that width
having been adopted by George Stephenson in the construction of the
earlier lines. Brunel, the engineer of the Great Western, adopted, however,
in the construction of that railway, a gauge of 7 ft., with a view of obtaining
greater speed and power in the engines, steadiness in the carriages,
and increased size of carriages for bulky goods. The proposal to adopt
this gauge gave rise to a memorable dispute among engineers, often called
“The Battle of the Gauges.” It was stated that any advantages of the
broad gauge were more than compensated by its disadvantages. The want
of uniformity in the gauges was soon felt to be an inconvenience to the
public, and a Parliamentary Committee was appointed to consider the
subject. They reported that either gauge supplied all public requirements,
but that the broad gauge involved a great additional outlay in its construction
without any compensating advantages of economy in working; and,
as at that time 2,000 miles of railway had been constructed on the narrow
gauge, whereas only 270 miles were in existence on the broad gauge, they
recommended that future railways should be made the prevailing width of
56½ in. The Great Western line had engines, bridges, tunnels, viaducts,
&c., on a larger scale than any other railway in Britain. The difference of
gauge was after a time felt to involve so much inconvenience that lines
which adopted the 7–ft. gauge have since relaid the tracks at the more
common width. At the present day we find the Great Western Railway
completely reconstructed on the narrow gauge system, in order that trains
may run without interruption in connection with other lines.
Fig. 45.—Conical Wheels.
Fig. 46.—Centrifugal Force.
The wheels of railway carriages and engines differ from those of ordinary
107carriages in being fastened in pairs upon the axles, with which they revolve
(see Fig. 45). The tire of the wheel is conical, the slope being about
1 in 20; that is, in a
wheel 5 in. broad the
radius of the outer edge
is ¼ in. less than that of
the inner; and the rails
are placed sloping a
little inwards. The
effect of this conical
figure is to counteract
any tendency to roll off
the rails; for if a pair
of wheels were shifted
a little to one side, the
parts of the tires rolling
upon the rails being
then of unequal circumference,
would cause the
wheels to roll towards
the other side. The
conical shape produces
this kind of adjustment so well that the flanges do not in general touch the
rails. They act, however, as safeguards in passing over curves and junctions.
In curves the outer line of rails is laid higher than the inner, so that
in passing over them the train leans slightly inwards, in order to counteract
what is called the centrifugal
force, to which any body moving
in a curve is subject. This so-called
force is merely the result
of that tendency which every
moving body has to continue its
motion in a straight line. A very
good example of the effect of this
may be seen when a circus horse
is going rapidly round the ring.
The inclination inwards is still
more perceptible when a rider is
standing on the horse’s back, as
shown in Fig. 46. The earth’s
attraction of gravity is pulling
the performer straight down,
and the centrifugal force would
of itself throw her outwards horizontally.
The resultant or combined
effect of both acts is seen
in the exact direction in which
she is leaning, and it presses her
feet on the horse’s back, the
animal itself being under similar
conditions. It is obvious that
the amount of centrifugal force, and therefore of inward slope, will increase
with the speed and sharpness of the curve, and on the railways the rails
108are placed so that the slope counteracts the centrifugal force when the
train travels at about the rate of twenty miles per hour.
Fig. 47.—Points.
A very important part of the mechanism of a railway is the mode of
passing trains from one line of rails to another. Engines and single carriages
are sometimes transferred by means of turn-tables, but the more
general plan is by switches, which are commonly constructed as shown in
Fig. 47. There are two rails, A and B, tapering to a point and fixed at the
other end, so that they have sufficient freedom to turn horizontally. A
train passing in the direction shown by the arrow would continue on the
main line, if the points are placed as represented; but if they be moved
so that the long tongue is brought into contact with the rail of the main
line, then the train would run on to the side rails. These points are worked
by means of a lever attached to the rod, C, the lever being either placed
near the rails, or in a signal-box, where a man is stationed, whose sole duty
it is to attend to the points and to the signals. The interior of a signal-box
near an important junction or station is shown in Fig. 48, and we see
here the numerous levers for working the points and the signals, each of
these having a connection, by rods or wires, with the corresponding point
or signal-post. The electric telegraph is now an important agent in railway
signalling, and in a signal-box we may see the bells and instruments which
inform the pointsman whether a certain section of the line is “blocked” or
“clear.” The signals now generally used on British railways are made by
the semaphore, which is simply a post from which an arm can be made to
project. When the driver of the train sees the arm projecting from the
left-hand side of the post, it is an intimation to him that he must stop his
train; when the arm is dropped half-way, so as to project 45° from the post,
it is meant that he must proceed cautiously; when the arm is down the
line is clear. These signals, of course, are not capable of being seen at night,
when their place is supplied with lamps, provided with coloured glasses—red
and green—and also with an uncoloured glass. The lamp may have
the different glasses on three different sides, and be turned round so as to
present the required colour; or it may be made to do so without turning,
if provided with a frame having red and green glasses, which can be moved
109like spectacles in front of it. The meanings of the various coloured lights
and the corresponding semaphore signals are these:
White
All right
Go on.
Green
Caution
Proceed slowly.
Red
Danger
Stop.
Fig. 48.—Signal-box on the North London Railway.
A very clear account of the mode of working railway signals on what is
now called the block system, together with a graphic description of a signal-box,
was given in a paper which appeared some years ago in “The Popular
Science Review,” from the pen of Mr. Charles V. Walker, F.R.S., the
telegraph engineer to the South-Eastern Railway Company, who was the
first to organize an efficient system of electric signalling for railways. We
may remark that the signalling instruments on the South-Eastern line, and
indeed on all the lines at the present day, address themselves both to the
ear and to the eye, for they consist of—first, bells, on which one, two, or
more blows are struck, each series of blows having its own particular
meaning; and, second, of a kind of miniature signal-post, with arms capable
of being moved by electric currents into positions similar to those of the
arm of an actual signal-post, so that the position of the arms is made always
to indicate the state of the line. One arm of the little signal-post—the left—is
red, and it has reference to receding trains; the other—viz., the right—arm
is white, and relates to approaching trains. Mr. Walker thus describes
the signalling:
110“The ordinary position of the arms of the electro-magnetic telegraph
semaphores will be down; that is to say, when the line is clear of all trains,
and business begins, say in early morning, all the arms will be down, indicating
that no train is moving. When the first train is ready to start, say
from Charing Cross, the signalman will give the proper bell-signal to Belvidere—two,
three, or four blows, according as the train is for Greenwich,
for North Kent, or Mid-Kent, or for the main line; and the Belvidere man
will acknowledge this by one blow on the bell in reply, and without raising
the Charing Cross red or left arm. This is the signal that the train may
go on; and when the train has passed, so that the Charing Cross man can
see the tail lights, he gives the out signal a second time, which the Belvidere
man acknowledges, at the same time raising the red arm at Charing Cross,
behind the train, and so protecting it until it has passed him at Belvidere,
when he signals to that effect to Charing Cross, at the same time putting
down the red arm there, as an indication that the line is again clear. While
these operations are going on for down trains, others precisely similar, but
in the reverse direction, are going on for up trains.... One and the
same pressure on the key sends a bell signal and raises or depresses the
semaphore arm as the case may require, a single telegraph wire only being
required for the combined system, as for the more simple bell system.”
In one of the signal-boxes on the South-Eastern line, Mr. Walker states,
on a certain day 650 trains or engines were signalled and all particulars
accurately entered in a book, the entries requiring the writing down of
nearly 8,000 figures: an illustration of the amount of work quietly carried
on in a signal-box for the advantage and security of the travelling public.
Mr. Walker also gives us a peep into the inside of one of the signal-boxes,
thus: “The interior of a large signal-box exhibits a very animated scene,
in which there are but two actors, a man and a boy, both as busy as bees,
but with no hurry or bustle. The ruling genius of the place is the strong,
active, intelligent signalman, standing at one end of the apartment, the
monarch for the time being of all he surveys. Immediately before him in
one long line, extending from side to side, is a goodly array of levers, bright
and clean from constant use and careful tending, each one labelled for its
respective duty. Before him to the right and left are the various electro-magnetic
semaphores, each one in full view and adjusted in position to the
pair of roads to which it is appropriated, and all furnished with porcelain
labels. Directly in front of him is a screen, along which are arranged the
various semaphore keys; and on brackets, discreetly distributed, are the
bells and gongs, the twin companions each of its own semaphore. Before
the screen are the writing-desk and books, and here stands the youngster,
the ministering spirit, all on the alert to take or to send electric signals and
to record them, his time and attention being devoted alternately to his
semaphore keys and to his books, being immediately under the eye and
control of the signalman. This is no place for visitors, and the scenes
enacted here have little chance of meeting the public gaze; indeed, the
officers whose duties take them hither occasionally are only too glad to
look on, and say as little as may be, and not interrupt the active pair, between
whom there is evidently a good understanding in the discharge of
duties upon the accurate performance of which so much depends. Looking
on, the man will be seen in command of his rank and file: signals come,
are heard and seen by both man and boy; levers are drawn and withdrawn,
one, two, three, or more; the arms and the lamps on the gigantic
masts outside, of which there are three, well laden, are displayed as required,
111distant signals are moved, points are shifted and roads made ready;
telegraph signals are acknowledged; and on looking out—for the box is
glazed throughout—trains are seen moving in accordance with the signals
made; and on the signal-posts at the boxes, right and left—for here they
are within easy reach of each other—arms are seen up and down in sympathy
with those on the spot, and with the telegraph signals that have been
interchanged. There is no cessation to this work, and there is no confusion
in it; one head and hand directs the whole, so that there are no conflicting
interests and no misunderstandings; all is done in perfect tranquillity,
and the great secret is that one thing is done at a time. All this,
which is so simple and so full of meaning to the expert, is to the uninitiated
intricate and vague; and though he cannot at first even follow the description
of the several processes, so rapidly are they begun and ended, yet, as
the cloud becomes thin, and his ideas become clearer, he cannot fail to be
gratified, and to be filled with admiration at the great results that are
brought about by means so simple.”
Fig. 49.—Post Office Railway Van.
Most of the carriages used on railways are so familiar to everyone that
it is unnecessary to give any description of them. We give a figure of
one which, though of early type, has special features of interest, being the
well-designed Travelling Post Office, Fig. 49. In such vans as that here
represented letters are sorted during the journey, and for this purpose the
interior is provided with a counter and with pigeon-holes from end to end.
When the train stops bags may, of course, be removed from or received
into the van in the ordinary manner; but by a simple mechanism bags
may be delivered at a station and others taken up while the train continues
its journey at full speed. A bar can be made to project from the side of
the carriage, and on this the bag is hung by hooks, which are so contrived
that they release the bag when a rod, projecting from the receiving apparatus,
strikes a certain catch on the van. The bag then drops into a netting,
which is spread for its reception; and in order to receive the bags taken
up, a similar netting is stretched on an iron frame attached to the van
112This frame is made to fold up against the side of the carriage when not in
use. When the train is approaching the station where the bag is to be
taken up, this frame is let down, and a projecting portion detaches the
bags, so that they drop into the net, from which they are removed into
the interior of the vehicle. These travelling post offices are lighted with
gas, and are padded at the ends, so that the clerks may not be liable to
injury by concussions of the carriages.
England has had to borrow from the United States not a few hints
for such adaptations and appliances as tend to promote the comfort
and convenience of travellers by rail, especially on what we insularly
call long journeys. Some of these vehicles on the American railways
are luxurious hotels upon wheels; they contain accommodation for
forty persons, having a kitchen, hot and cold water, wine, china and
linen closets, and more than a hundred different articles of food, besides
an ample supply of tablecloths, table napkins, towels, sheets, pillowcases,
&c. Then there are other Pullman inventions, such as the “palace”
and the “sleeping” cars, in which the traveller who is performing a long
journey makes himself at home for days, or perhaps for a week, as, for instance,
while he is being carried across the American continent from ocean
to ocean at the easy rate of twenty miles an hour on the Pacific and other
connecting lines. Mr. C. Nordhoff, an American writer, giving an account
of his journey to the Western States, writes thus: “Having unpacked your
books and unstrapped your wraps in your Pullman or Central Pacific palace
car, you may pursue all the sedentary avocations and amusements of a
parlour at home; and as your housekeeping is done—and admirably done—for
you by alert and experienced servants; as you may lie down at full
length, or sit up, sleep, or wake at your choice; as your dinner is sure to
be abundant, very tolerably cooked, and not hurried; as you are pretty
certain to make acquaintances in the car; and as the country through
which you pass is strange and abounds in curious and interesting sights, and
the air is fresh and exhilarating—you soon fall into the ways of the voyage;
and if you are a tired business man or a wearied housekeeper, your careless
ease will be such a rest as certainly most busy and overworked Americans
know how to enjoy. You write comfortably at a table in a little room
called a ‘drawing-room,’ entirely closed off, if you wish it, from the remainder
of the car, which room contains two large and comfortable armchairs
and a sofa, two broad clean plate-glass windows on each side (which
may be doubled if the weather is cold), hooks in abundance for shawls,
hats, &c., and mirrors at every corner. Books and photographs lie on
the table. Your wife sits at the window sewing and looking out on long
ranges of snow-clad mountains or on boundless ocean-like plains. Children
play on the floor or watch at the windows for the comical prairie dogs sitting
near their holes, and turning laughable somersaults as the car sweeps
by. The porter calls you at any hour you appoint in the morning; he
gives half an hour’s notice of breakfast, dinner, or supper; and while you
are at breakfast, your beds are made up and your room or your section
aired. About eight o’clock in the evening—for, as at sea, you keep good
hours—the porter, in a clean grey uniform, comes in to make up the beds.
The two easy-chairs are turned into a berth; the sofa undergoes a similar
transformation; the table, having its legs pulled together, disappears in a
corner, and two shelves being let down furnish two other berths. The
freshest and whitest of linen and brightly-coloured blankets complete the
outfit; and you undress and go to bed as you would at home.”
113An important general truth may find a familiar illustration in the subject
now under notice. The truth in question may be expressed by saying that,
in all human affairs, as well as in the operations of nature, the state of
things at any one time is the result, by a sort of growth, of a preceding
state of things. And in this way it is certainly true of inventions, that
they never make their appearance suddenly in a complete and finished
state—like Minerva, who is fabled to have sprung from the brain of Jupiter
fully grown and completely armed; but rather their history resembles the
slow and progressive process by which ordinary mortals attain to their full
stature. We have already seen that railways had their origin in the tramways
of collieries; and, in like manner, the railway carriage grew out of the
colliery truck and the stage coach; for when railway carriages to convey
passengers were first made, it did not occur to their designers that anything
better could be done than to place coach bodies on the frame of the truck;
and accordingly the early railway carriages were formed by mounting the
body of a stage coach, or two or three such bodies side by side, on the
timber framework which was supported by the flanged wheels. The cut,
Fig. 56, is from a painting in the possession of the Connecticut Historical
Society, and it represents the first railway train in America on its trial trip
(1831), in which sixteen persons took part, who were then thought not a
little courageous. Here we see that the carriages were regular stage
coaches, and the same was the case in England. But it is very significant
that, to this day, the stage coach bodies are traceable in many of the carriages
now running on English lines, especially in the first-class carriages,
where, in the curved lines of the mouldings which are supposed to ornament
the outside, one may easily recognize the forms of the curved bodies
of the stage coaches, although there is nothing whatever, in the real framing
of the timbers of the railway carriage, which has the most distant relation
to these curves. Then again, almost universally on English lines, the old
stage coach door-handles are still retained on the first-class carriages,
in the awkward flat oval plates of brass which fold down with a hinge.
Many other points might be named which would show the persistence of
the stage coach type on the English railways. The cut, Fig. 56, proves
that the Americans set out with the same style of carriages; but North
America, as compared with the Old World, is par excellence the country of
rapid developments, and there carriages, or cars, as our Transatlantic
cousins call them, have for a long time been made with numerous improvements,
and in forms more in harmony with the railway system, than the
conservatism of English ideas, still cleaving to the stage coach type, permitted
to be attempted in this country.
Railway travellers in the United States had long enjoyed the benefit
of comforts and convenience in the appointments of their carriages long
before any change had been effected in the general arrangements of the
vehicles provided by the railway companies in England. It is now indeed
a considerable number of years since this state of things has been altered
in the older country; as all the great lines, following the example of the
Midland Company, who first adopted the Pullman cars, have constructed
luxurious vehicles in which every elegance and comfort are placed within
the reach of the English traveller, and these improvements are highly
appreciated by all who have long journeys to make by day or night.
The elegance and comfort of the arrangements are almost too obvious to
require description. We see the luxuriously padded chairs, which, by
turning on swivels, permit the traveller to adjust his position according to
his individual wishes, so that he can, with ease, place his seat either to gaze
114directly on the passing landscape, or turn his face towards his fellow-travellers
opposite or on either side. The chairs are also provided with
an arrangement for placing the backs at any required inclination, and the
light and refined character of the decorations of the carriage should not
escape the reader’s notice. Pullman Cars of another kind, providing
sleeping accommodation for night journeys, are also in use on the Midland
line, and they are fitted up with the same thoughtful regard to comfort as
the Parlour Car.
The great engineering feats which have been accomplished in the construction
of railways are numerous enough to fill volumes. We give, therefore,
only a short notice of one or two recently constructed lines which have
features of special interest, concluding with a brief account of such
remarkable constructions as the railway by which the traveller may now
go up the Rigi, and the railways which ascend Vesuvius and Mt. Pilatus.
When the traffic in the streets of London became so great that the
ordinary thoroughfares were unable to meet public requirements, the
bold project was conceived of making a railway under the streets. The construction
of a line of railway beneath the streets of a populous city, amidst a
labyrinth of gas-pipes, water-mains, sewers, &c., is obviously an undertaking
presenting features so remarkable that the London Underground Railway
cannot here be passed over without a short notice. Its construction occupied
about three years, and it was opened for traffic in 1863. The line
commencing at Paddington, and passing beneath Edgware Road at right
angles, reaches Marylebone Road, under the centre of which it proceeds,
and passing beneath the houses at one end of Park Crescent, Portland
Place, it follows the centre of Euston Road to King’s Cross, where connection
with the Great Northern and Midland system is effected. Here the
line bends sharply southwards, and proceeds to Farringdon Street Station,
the original terminus. A subsequent extension takes an easterly direction
and reaches Aldgate Station, the nominal terminus. The crown of the
arch which covers the line is in some places only a few inches beneath the
level of the streets; in other places it is several feet below the surface, and,
in fact, beneath the foundations of the houses and other buildings. The
steepest gradient on the line is 1 in 100, and the sharpest curve has a
radius of 200 yards. The line is nearly all curved, there not being in all
its length three-quarters of a mile of straight rails. The difficulties besetting
an undertaking of this kind would be tedious to describe, but may readily
be imagined. The line traverses every kind of soil—clay, gravel, sand,
rubbish, all loosened by previous excavations for drains, pipes, foundations,
&c.; and the arrangements of these drains, water and gas-pipes, had to
be reconciled with the progress of the railway works, without their uses
being interfered with even for a time. Of the stations the majority have
roofs of the ordinary kind, open to the sky; but two of them, namely,
Baker Street and Gower Street, are completely underground stations, and
their roofs are formed by the arches of brickwork immediately below the
streets. The arrangements at these stations show great boldness and
115inventiveness of design. The booking offices for the up line are on one
side of the road, and those for the down line on the other. Fig. 50 represents
the interior of the Gower Street Station, and the other is very similar.
In each the platforms are 325 ft. long and 10 ft. broad, and the stations
are lighted by lateral openings through the springing of the arch which
forms the roof. This arch is a portion of a circle of 32 ft. radius, with a
span of 45 ft. and a rise of 9 ft. at the crown. The lateral openings are
arched at the top and bottom, but the sides are flat. The width of each is
4 ft. 9 in., and the height outside 6 ft., increasing to 10 ft. at the ends
opening on the platform. The openings are entirely lined with white glazed
tiles, and the outward ends open into an area, the back of which is inclined
at an angle of 45°, and the whole also lined with white glazed tiles, and
covered with glass, except where some iron gratings are provided for ventilation.
The tiles reflect the daylight so powerfully that but little gas is
required for the illumination of the station in the day-time. The arched
roofs of these stations are supported by piers of brickwork, 10 ft. apart,
5 ft. 6 in. deep, and 3 ft. 9 in. wide. In the spaces between the piers vertical
arches, like parts of the brick lining of a well, are wedged in, to resist the
thrust of the earth, and a straight wall is built inside of this between the
piers, to form the platform wall of the station. The tops of the piers are
connected by arches, and are thus made to bear the weight of the arched
roof, which has 2 ft. 3 in. thickness of brickwork at the crown, and a much
greater thickness towards the haunches.
Fig. 50.—Gower Street Station, Metropolitan Railway.
The benefit derived by the public from the completion of the Metropolitan
Railway was greatly increased by the subsequent construction of another
railway—“The Metropolitan District,” which, joining the Metropolitan at
Paddington, makes a circuit about the west-end of Hyde Park, and passing
close to the Victoria Terminus of the London, Chatham, and Dover and
the Brighton and South Coast Railways, reaches Westminster Bridge, and
then follows the Thames Embankment to Blackfriars Bridge, where it
116leaves the bank of the river for the Mansion House, Mark Lane and
Aldgate stations. This line, taken in conjunction with the Metropolitan,
forms the “inner circle” of the railway communication in London. The
circuit was for a long time incomplete at the east by the want of connection
between the Mansion House Station and that of Moorgate Street,
although these stations are but little more than half a mile apart. A line
connecting these two points has lately been constructed at great cost,
and the public now possess a complete circle of communication. The
number of trains each day entering and leaving some of the stations on
the Metropolitan system is very great. Moorgate Street Station—a
terminus into which several companies run—may have about 800 trains
arriving or departing in the course of a day.
The remarkable development of railways which has taken place in the
United States has its most striking illustration in the great system of
lines by which the whole continent can be traversed from shore to shore.
The distance by rail from New York to San Francisco is 3,215 miles, and
the journey occupies about a week, the trains travelling night and day. The
traveller proceeding from the Eastern States to the far west has the choice
of many routes, but these all converge to Omaha. From this point the
Pacific Railroad will convey him towards the land of the setting sun. The
map, Fig. 51, shows the course of this railway, which is the longest in the
world. It traverses broader plains and crosses higher mountains than any
other. Engineering skill of the most admirable kind has been displayed
in the laying-out and in the construction of the line, with its innumerable
cuttings, bridges, tunnels, and snow-sheds.
Fig. 51.—Map of the Route of the Pacific Railway.
The road from Omaha to Ogden, near the Great Salt Lake—a distance
of 1,032 miles—is owned by the Union Pacific Company, and the Central
Pacific joins the former at Ogden and completes the communication to
San Francisco, a further length of 889 miles—the whole distance from
Omaha to San Francisco being 1,911 miles. The Union Pacific was commenced
in November, 1865, and completed in May, 1869. There are at
Omaha extensive workshops provided with all the appliances for constructing
and repairing locomotives and carriages, and these works cover 30 acres
of ground, and give employment to several thousand men. The population
of Omaha rose during the making of the railway from under 3,000 in 1864
to more than 16,000 in 1870, and it is now a flourishing town. A little distance
from Omaha the line approaches the Platte River, and the valley of
this river and one of its tributaries is ascended to Cheyenne, 516 miles
from Omaha, the line being nowhere very far from the river’s course.
Cheyenne is 5,075 ft. higher above the sea than Omaha, the elevation of
which is 966 ft. The Platte River is a broad but very shallow stream, with
a channel continually shifting, owing to the vast quantity of sand which its
muddy waters carry down. This portion of the line passing through a district
where leagues upon leagues of fertile land await the hand of the tiller,
has opened up vast tracts of land—hedgeless, gateless green fields, free to
all, and capable of receiving and supporting millions of human inhabitants.
117Cheyenne, a town of 3,000 inhabitants,
is entirely the creation of the railways,
for southward from Cheyenne a railway
passes to Denver, a distance of 106
miles, through rich farming and grazing
districts. Seven miles beyond Cheyenne
the line begins to ascend the Black Hills
by steep gradients, and at Granite Canyon,
for example, the rise in five miles
is 574 ft., or about 121 ft. per mile. Many
lime-kilns have been erected in this
neighbourhood, where limestone is very
abundant. A little beyond this point
the road is in many places protected by
snow-sheds, fences of timber, and rude
stonework. At Sherman, 549 miles
from Omaha, the line attains the summit
of its track over the Black Hills,
and the highest point on any railway
in the world, being 8,242 ft. above the
level of the sea. Wild and desolate
scenery characterizes the district round
Sherman, and the hills, in places covered
with a dense growth of wood, will
furnish an immense supply of timber
for years to come. The timber-sheds
erected over the line, and the fences
beside it are not so much on account of
the depth of snow that falls, but to prevent
it from blocking the line by being
drifted into the cuts by the high wind.
A few miles beyond Dale Creek at Sherman
is the largest bridge on the line.
It is a trestle bridge, 650 ft. long and
126 ft. high, and has a very light appearance—indeed,
to an English eye
unaccustomed to these impromptu
timber structures, it looks unpleasantly
light. From Sherman the line descends
to Laramie, which is 7,123 ft. above the
sea level and 24 miles from Sherman,
and here the railway has a workshop,
for good coal is found within a few
miles. A fine tract of grazing land,
60 miles long and 20 miles broad,
stretches around this station, and it is
said that nowhere in the whole North
American continent can cattle be reared
and fattened more cheaply. The line,
now descending the Black Hills, crosses
for many miles a long stretch of rolling
prairie, covered in great part with sage-bush,
and forming a tableland lying between
118the western base of the Black Hills and the eastern base of the
snowy range of the Rocky Mountains, which latter reach an elevation of
from 10,000 to 17,000 ft. above the sea level and are perpetually covered
with snow. Such tablelands are termed in America “parks.” Before the
line reaches the summit of the pass by which it crosses the range of the
snowy mountains, it traverses some rough country among the spurs of the
hills—through deep cuts and under snow-sheds, across ravines and rivers,
and through tunnels. At Percy, 669 miles, is a station named after Colonel
Percy, who was killed here by the Indians when surveying for the line. He
was surprised by a party of the red men, and retreated to a cabin, where
he withstood the attack of his assailants for three days, killing several of
them; but at length they set fire to the cabin, and the unfortunate Colonel
rushing out, fell a victim to their ferocity. Near Creston, 737 miles from
Omaha, the highest point of the chief range is reached, though at an
elevation lower by 1,212 ft. than the summit of the pass where the line
crosses the Black Hills, which are the advanced guard of the Rocky
Mountains. Here is the water-shed of the continent, for all streams rising
to the east of this flow ultimately into the Atlantic,—while these, having
their sources in the west, fall into the Pacific. Before reaching Ogden the
line passes through some grand gorges, which open a way for the iron
119horse through the very hearts of the mountains, as if Nature had foreseen
railways and providently formed gigantic cuttings—such as the Echo and
Weber Canyons, which enable the line to traverse the Wahsatch Mountains.
Fig. 52.—Trestle Bridge.
Echo Canyon is a ravine 7 miles long, about half a mile broad, flanked
by precipitous cliffs, from 300 to 800 ft. high, and presenting a succession
of wild and grand scenery. In Weber Canyon the river foams and rushes
along between the mountains, which rise in massive grandeur on either
side, plunging and eddying among the huge masses of rock fallen from
the cliffs above. Along a part of the chasm the railway is cut in the side
of the steep mountain, descending directly to the bed of the stream.
Where the road could not be carried round or over the spurs of the mountains
it passes through tunnels, often cut through solid stone. A few miles
farther the line reaches the city of Ogden, in the state of Utah, the territory
of the Mormons. This territory contains upwards of 65,000 square miles,
and though the land is not naturally productive, it has, by irrigation, been
brought into a high state of cultivation, and it abounds in valuable minerals,
so that it now supports a population of 80,000 persons.
Fig. 53.—American Canyon.
We have now arrived at Ogden, where the western portion of the great
railway line connecting the two oceans unites to the Union Pacific we have
just described. This western portion is known as the Central Pacific Railroad,
and it stretches from Ogden to San Francisco, a distance of 882
miles.
The portion of the line which unites Sacramento to Ogden, 743 miles,
was commenced in 1863 and finished in 1869, but nearly half of the entire
length was constructed in 1868, and about 50 miles west of Ogden, the remarkable
engineering feat of laying 10 miles of railway in one day was
performed. It was thus accomplished: when the waggon loaded with the
120rails arrived at the end of the track, the two outer rails were seized, hauled
forward off the car, and laid upon the sleepers by four men, who attended
to this duty only. The waggon was pushed forwards over these rails, and
the process of putting down the rails was repeated, while behind the waggon
came a little army of men, who drove in the spikes and screwed on the fish-plates,
and, lastly, a large number of Chinese workmen, with pickaxes and
spades, who ballasted the line. The average rate at which these operations
proceeded was about 240 ft. of track in 77½ seconds, and in these 10
miles of railway there were 2,585,000 cross-ties, 3,520 iron rails, 55,000
spikes, 7,040 fish-plates, and 14,080 bolts with screws, the whole weighing
4,362,000 lbs.! Four thousand men and hundreds of waggons were required,
but in the 10 miles all the rails were laid by the same eight men,
each of whom is said to have that day walked 10 miles and lifted 1,000 tons
of iron rails. Nothing but the practice acquired during the four previous
years and the most excellent arrangement and discipline could have made
the performance of such a feat possible as the laying of eight miles of the
track in six hours, which was the victory achieved by these stalwart navvies
before dinner.
The line crosses the great American desert, distinguished for its desolate
aspect and barren soil, and so thickly strewn with alkaline dust that it
appears almost like a snow-covered plain. The alkali is caustic, and where
it abounds no vegetation can exist, most of the surface of this waste being
fine, hard grey sand, mixed with the fragments of marine shells and beds
of alkali.
The third great mountain range of the North American continent is
crossed by this line, at an elevation of 7,043 ft. above the sea level. The
Sierra Nevada, as the name implies, is a range of rugged wild broken
mountain-tops, always covered with snow. The more exposed portions of
the road are covered with snow-sheds, solidly constructed of pine wood
posts, 16 in. or 20 in. across: the total length of snow-sheds on the Sierra
Nevada may equal 50 miles. These sheds sometimes take fire; but the
company have a locomotive at the Summit Station, ready to start at a
moment’s notice with cars carrying tanks of water. The snow falls there
sometimes to a depth of 20 ft. in one winter; and in spring, when it falls
into the valleys in avalanches, sweeping down the mountain-sides, they pass
harmlessly over the sloping roofs of the snow-sheds. Where the line passes
along the steep flank of a mountain, the roofs of these snow-sheds abut
against the mountain-side, so that the masses of snow, gliding down from
its heights, continue their slide without injury to line, or sheds, or trains.
Where, however, the line lies on level ground, or in a ridge, the snow-sheds
are built with a strong roof of double slope, in order to support or throw off
the snow. From Summit (7,017 ft.) the line descends continuously to
Sacramento, which is only 30 ft. above the sea level, and 104 miles from
Summit. About 36 miles from Summit, the great American Canyon, one
of the wildest gorges in the Sierra Nevada range, is passed. Here the
American River is confined for a length of two miles between precipitous
walls of rock, 2,000 ft. in height, and so steep that no human foot has ever
yet followed the stream through this tremendous gorge (Fig. 53). A few
miles beyond this the line is carried, by a daring feat of engineering, along
the side of a mountain, overhanging a stream 2,500 ft. below. This mountain
is known as “Cape Horn,” and is a place to try the nerves of timid
people. When this portion of the line was commenced, the workmen were
lowered and held by ropes, until they had hewn out a standing-place on
121the shelving sides of the precipice, along whose dizzy height, where even
the agile Indian was unable to plant his foot, the science of the white man
thus made for his iron horse a secure and direct road. (Fig. 54.)
Fig. 54.—“Cape Horn.”
Fig. 55.—Snow Plough.
These lines of railway, connecting Omaha with Sacramento, are remarkable
evidences of the energy and spirit which characterize the Anglo-Saxon
race in America. The men who conceived the design of the Central Pacific
Railroad, and actually carried it into effect, were not persons experienced
in railway construction; but five middle-aged traders of Sacramento, two of
whom where drapers, one a wholesale grocer, and the others ironmongers,
believing that such a railway should be made, and finding no one ready
to undertake it, united together, projected the railway, got it completed,
and now manage it. These gentlemen were associated with an engineer
122named Judah, who was a sanguine advocate of the scheme, and made the
preliminary surveys, if he did not plan the line. The line is considered
one of the best appointed and best managed in the States; yet the project
was at first ridiculed and pronounced impracticable by engineers of high
repute, opposed by capitalists, and denounced by politicians. An eminent
banker, who personally regarded the scheme with hopefulness, would not
venture, however, to take any stock, lest the credit of his bank should be
shaken, were he known to be connected with so wild a scheme. And,
indeed, the difficulties appeared great. Except wood, all the materials
required, the iron rails, the pickaxes and spades, the waggons, the locomotives,
and the machinery had to be sent by sea from New York, round
Cape Horn, a long and perilous voyage of nine months duration, and
transhipped at San Francisco for another voyage of 120 miles before they
could reach Sacramento. Add to this that workmen were so scarce in
California, and wages so high, that to carry on the work it was necessary
to obtain men from New York; and during its progress 10,000 Chinamen
were brought across the Pacific, to work as labourers. Subscriptions came
in very slowly, and before 30 miles of the line had been constructed, the
price of iron rose in a very short time to nearly three times its former
amount. At this critical juncture, the five merchants decided to defray,
out of their own private fortunes, the cost of keeping 800 men at work on
the line for a whole year. We cannot but admire the unswerving confidence
in their enterprise displayed by these five country merchants, unskilled in
123railway making, unaided by public support, and even discouraged in their
project by their own friends. The financial and legal obstacles they successfully
surmounted were not the only difficulties to be overcome. They
had the engineering difficulties of carrying their line over the steep Sierra,
a work of four years; long tunnels had to be bored; one spring when snow
60 ft. in depth covered the track, it had to be removed by the shovel for 7
miles along the road; saw-mills had to be erected in the mountains, to prepare
the sleepers and other timber work; wood and water had to be carried
40 miles across alkali plains, and locomotives and rails dragged over the
mountains by teams of oxen. The chief engineer, who organized the force
of labourers, laid out the road, designed the necessary structures, and successfully
grappled with the novel problem of running trains over such a
line in all seasons, was Mr. S. S. Montague. The requirements of the
traffic necessitate not only solidly constructed iron-covered snow-sheds,
but massive snow-ploughs to throw off the track the deep snow which could
in no other way be prevented from interrupting the working of the line.
These snow-ploughs are sometimes urged forward with the united power of
eight heavy locomotives. Fig. 55 represents one of these ploughs cleaning
the line, by throwing off the snow on to the sides of the track. The cutting
apparatus varies in its arrangements, some forms being designed to push the
snow off on one side, some on the other, and to fling it down the precipices;
and others, like the one represented, are intended merely to throw it off
the track.
Fig. 56.—The first Steam Railroad Train in America.
Sacramento is 1,775 miles from Omaha, and is connected with San Francisco
by a line 139 miles long. At San Francisco, or rather at Oakland,
1,911 miles from Omaha and 3,212 miles from New York, is the terminus
of the great system of lines connecting the opposite shores of the vast
North American continent. San Francisco, situated on the western shore
of a bay, is connected with Oakland by a ferry; but the railway company
have recently constructed a pier, which carries the trains out into the bay
for 2¼ miles. This pier is strongly built, and is provided with a double set
of rails and a carriage-road, and with slips at which ships land and embark
passengers, so that ships trading to China, Japan, and Australia can
load and unload directly into the trains, which may pass without change
from the shores of the Pacific to those of the Atlantic Ocean. San Francisco
is a marvellous example of rapid increase, for the population now
numbers 170,000, yet a quarter of a century ago 500 white settlers could
not be found in as many miles around its site. The first house was erected
in 1846, and in 1847 not a ship visited the bay, but now forty large steamships
ply regularly, carrying mails to China, Japan, Panama, South America,
Australia, &c., and there are, of course, hundreds of other steamers and
ships.
124The descriptions we have given of only two lines of railway may suffice
to show that the modern engineer is deterred by no obstacles, but boldly
drives his lines through places apparently the most impracticable. He
shrinks from no operations however difficult, nor hesitates to undertake works
the mere magnitude of which would have made our forefathers stand aghast.
Not in England or America alone, but in almost every part of the world,
the railways have extended with wonderful rapidity; the continent of Europe
is embraced by a network of lines; the distant colonies of Australia and
New Zealand have thousands of miles of lines laid down, and many more
in progress; the map of India shows that peninsula traversed in all directions
by the iron roads; and in the far distant East we hear of Japan having
several lines in successful operation, and the design of laying down more.
In connection with such works, at home and abroad, many constructions
of great size and daring have been designed and erected; many navigable
rivers have been bridged, and not seldom has an arm of the sea itself been
spanned; hundreds of miles of embankments and viaducts have been
raised; hills have been pierced with innumerable cuttings and tunnels, and
all these great works have been accomplished within the experience of a
single generation of men, and have sprung from one single successful
achievement of Stephenson’s—the Liverpool and Manchester Railway,
completed and opened in 1830. We in England should also have pride
in remembering that the growth of the railways here is due to the enterprise,
industry, and energy of private persons; for the State has furnished
no funds, but individuals, by combining their own resources, have executed
the works, and manage the lines for their common interest and the public
good. It is said that the amount of money which has been spent on railways
in Great Britain is not far short of 500 millions of pounds sterling. The
greatest railway company in the United Kingdom is the London and North-Western,
which draws in annual receipts about seven millions of pounds;
and the total receipts of all the railway companies would nearly equal half
the revenue of the State.
Fig. 57.—Railway Embankment near Bath.
PLATE VI.
MOUNT WASHINGTON INCLINED TRACK.
125
The construction of railways over lofty ranges of mountains will be
found illustrated by the brief notices in other pages of the Union Pacific
line in the United States, and of the St. Gothard railway over the Alps.
In such cases, the track has been to a great extent carried over the spurs
or along the sides of the mountains, so that such inclines might be obtained
as the ordinary locomotive was capable of ascending. The expensive
operation of tunnelling was resorted to only where sinuous deviations
from the more direct route involved a still greater expenditure of initial
cost, or a continual waste of time and energy in the actual working of the
line. Sometimes winding tracks, almost returning by snake-like loops on
their own route, as projected on the map, were required in order that the
ascent could be made with an incline practicable for the ordinary locomotive.
In the earlier development of railways, there were to be met
with cable inclines, where the traction of the locomotive had to be superseded
or supplemented by that of a rope or chain wound round a drum
actuated by a stationary steam-engine. The more powerful locomotives
of the present day are able to mount grades of such inclination that the
employment of cable traction is no longer requisite, except in but a few
cases. Railways had carried passengers about in all parts of the world
for many years before the engineer addressed himself to the problem of
easily and quickly taking people up heights of steep and toilsome ascent,
sought generally for the sake of the prospect, etc. Such, at least, has
been the object of most of the inclined railways already constructed, but
to this their utility is by no means limited, and as their safety and
stability has been proved by many years of use, they may find wider
applications than the gratification of the tourist and pleasure-seeker.
The toothed rail or rack which was formerly supposed necessary to
obtain power of traction on rails has been already mentioned (p. 101), and
as early as 1812 such a contrivance appears to have been in use in England,
near Leeds, the invention of a Mr. Blenkinsop. This mode of
traction received no development or improvement worthy of notice until
Mr. S. Marsh constructed, in 1866, a railway ladder—for so it may be
called—for the ascent of Mount Washington in the United States. In
this case there was a centre rail formed of iron, angle iron laid between
and parallel to the metals on which ran the wheels of the carriages. In
this centre rail angle irons were connected by round bars of wrought iron,
which the teeth of a pinion of the locomotive engaged, so that a climbing
action, resembling somewhat that of a wheel entering on the successive
rounds of a ladder, was produced, and in this way an ascensive power
was obtained sufficient to overcome gravity, the gradient not much exceeding
a rise of one foot in three at any point (12 vertical to 32
horizontal). This railway was completed in 1869, and for more than a
quarter of a century it has carried thousands of tourists to the summit of
Mount Washington without a single fatal accident. This system of
ascending mountains was soon adopted in Europe with certain improvements,
for in 1870 an inclined railway was constructed to the summit of
the Rigi, in which a system of involute gearing was substituted for the
ladder-like rounds of Mr. Marsh. A certain vibratory action, due to the
successive engagements of the teeth in the central rack, which was somewhat
126disagreeable for passengers, was soon afterwards obviated in the
Abt system, in which two racks are used, with the teeth of one opposite
the spaces of the other, and a double pinion provided, so that greater
uniformity in the acting power is obtained. With certain modifications
in detail, such as horizontal instead of vertical pinions, this system has
been largely adopted wherever cables have been dispensed with. In the
inclined railway by which Mount Pilatus, near Lucerne, is now ascended,
horizontal teeth project from both sides of a centre rail, and these are
engaged by horizontal pinions. The incline here is very steep, being in
places nearly 30 degrees; teeth perpendicular to the plane of the incline
would have offered a less margin of safety than those on the plan actually
adopted. In some places, as among the Alps, and more particularly in
South America, there are railways in which the ordinary mode of traction
and that with the rack are combined; that is, where the gradient exceeds
the ordinary limit, a central rack-rail is laid down, on approaching which
the engineer slackens his speed, and allows pinions, moved by the locomotive,
to become engaged in the double rack, by which he slowly climbs
the steep ascent until a level tract is reached which permits of the
ordinary traction being resumed.
Fig. 57a.—Train Ascending the Rigi.
Instead of climbing the inclines by rack-work rails, there is another
system which offers great advantages for economy in working, and one
generally resorted to where the incline can be made in one vertical plane.
This is the balanced cable, in which the gravitation force of a descending
car or train is utilised to draw up, or assist to draw up, the ascending car
or train. These cars are attached to the ends of a cable which passes
round a drum at the top of the incline, and means are provided, according
to circumstances, so that the drum may be turned, or its revolutions
127controlled by brakes. When there is a water supply at the upper end of
the incline, a simple and economical mode of working the cable is available;
for all that is necessary is to provide each car with a water-tank
capable of being rapidly filled and emptied. The upper car is made the
heavier when required, by filling its tank with water, when it raises the
lower car, and on itself arriving at the bottom, the water is discharged
before the load to be taken up is received.
Fig. 57b.—At the Summit of the Rigi.
Many inclined railways are now in operation in various parts of the
world, as at Mount Vesuvius, where two of the slopes have a combined
length of 10,500 feet; at Mount Supurga and at Mount San Salvatore
there are others. At Burgen-stock in Switzerland there is one having a
slope 57 feet vertical to 100 feet horizontal. These are cable inclines; but
a rack is also used with a pinion regulated by a friction-brake to avoid
accident, in case of the cable parting. The largest inclined railway in
America is at the Catskill Mountains, where an ascent of 1,600 feet is
made in a horizontal distance of 6,780 feet. In this a novel plan has been
adopted for compensating the varying weight that has to be moved, for
it is obvious that at the commencement the load at the top of the incline
has to raise not only that at the bottom, but the whole weight of the cable
128also, equal to 35,000 pounds of wire rope, and again after the middle point
has been passed, the descending power is constantly increasing, while
the load being raised is diminishing. Now, in order that the engine may
work with more uniform effect, the engineer has not made the incline a
straight line, but with the slope lightest at the bottom and gradually increased
towards the top, so that the line is really a curve in the vertical
plane, and has at every point just the inclination required for balancing
the weight of the wire cable, as this shifts from the one track to the other.
Instead of a rack pinion and brake to control a too rapid descent from
any accident, the cars are provided with clutches, which are automatically
thrown out on wooden guard-rails, when a safe speed is exceeded. Inclined
railways have also been constructed to the summit of Snowdon, in
North Wales, and to that of the Jungfrau, in Switzerland.
PLATE VII.
PIKE’S PEAK RAILWAY, ROCKY MOUNTAINS.
129
Fig. 58.—The Great Eastern at Anchor.
STEAM NAVIGATION. — THE RIVER AND LAKE STEAM-BOATS OF AMERICA.
The first practically successful steamboat was constructed by Symington,
and used on the Forth and Clyde Canal in 1802. A few years afterwards
Fulton established steam navigation in American waters, where a
number of steamboats plied regularly for some years before the invention
had received a corresponding development in England, for it was not until
1814 that a steam-packet ran for hire in the Thames. From that time, however,
the principle was quickly and extensively applied, and steamers made
their appearance on the chief rivers of Great Britain, and soon began also
to make regular passages from one sea-port to another, until at length, in
1819, a steamer made the voyage from New York to Liverpool. It does not
appear, however, that such ocean steam voyages became at once common,
for we read that in 1825 the captain of the first steam-ship which made the
voyage to India was rewarded by a large sum of money. It was not until
1838 that regular steam communication with America was commenced by
the dispatch of the Great Western from Bristol. Other large steamers were
soon built expressly for the passage of the Atlantic, and a new era in steam
navigation was reached when, in 1845, the Great Britain made her first
voyage to New York in fourteen days. This ship was of immense size,
compared with her predecessors, her length being 320 ft., and she was
130moreover made of iron, while instead of paddles, she was provided with
a screw-propeller, both circumstances at that time novelties in passenger
ships. Fulton appears to have made trial in America of various forms of
mechanism for propelling ships through the water. Among other plans he
tried the screw, but finally decided in favour of paddle-wheels, and for a
long time these were universally adopted. Many ships of war were built
with paddle-wheels, but the advantages of the screw-propeller were at length
perceived. The paddle-wheels could easily be disabled by an enemy’s
shot, and the large paddle-boxes encumbered the decks and obstructed the
operations of naval warfare. Another circumstance perhaps had a greater
share in the general adoption of the screw, which had long before been
proposed as a means of applying steam power to the propulsion of vessels.
This was the introduction of a new method of placing the screw, so that
its powers were used to greater advantage. Mr. J. P. Smith obtained a
patent in 1836 for placing the propeller in that part of the vessel technically
called the dead-wood, which is above the keel and immediately in
front of the rudder. When the means of propulsion in a ship of war is so
placed, this vital part is secure from injury by hostile projectiles, and the
decks are clear for training guns and other operations. Thus placed, the
screw has been proved to possess many advantages over paddle-wheels, so
that at the present time it has largely superseded paddle-wheels in vessels
of every class, except perhaps in those intended to ply on rivers and lakes.
Many fine paddle-wheel vessels are still afloat, but sea-going steamers are
nearly always now built with screw-propellers. In the application of the
steam engine to navigation the machine has received many modifications
in the form and arrangement of the parts, but in principle the marine
engine is identical with the condensing engine already described. The
engines in steam-ships are often remarkable for the great diameter given to
the cylinders, which may be 8 ft. or 9 ft. or more. Of course other parts of
the machinery are of corresponding dimensions. Such large cylinders require
the exercise of great skill in their construction, for they must be cast
in one piece and without flaws. The engraving, Fig. 59, depicts the scene
presented at the works of Messrs. Penn during the casting of one of these
large cylinders, the weight of which may amount to perhaps 30 tons. Only
the top of the mould is visible, and the molten iron is being poured in from
huge ladles, moved by powerful cranes. In paddle vessels the great wrought
iron shaft which carries the paddle-wheels crosses the vessel from side to
side. This shaft has two cranks, placed at right angles to each, and each
one is turned by an engine, which is very commonly of the kind known as
the side-lever engine. In this engine, instead of a beam being placed above
the cylinder, two beams are used, one being set on each side of the cylinder,
as low down as possible. The top of the piston-rod is attached to a crosshead,
from each end of which hangs a great rod, which is hinged to the
end of the side-beam. The other ends of the two beams are united by a
cross-bar, to which is attached the connecting-rod that gives motion to the
crank. Another favourite form of engine for steam-ships is that with oscillating
cylinders. The paddle-wheels are constructed with an iron framework,
to which flat boards, or floats, are attached, placed usually in a radial
direction. But when thus fixed, each float enters the water obliquely, and
in fact its surface is perpendicular to the direction of the vessel’s course only
at the instant the float is vertically under the axis of the wheel. In order to
avoid the loss of power consequent upon this oblique movement of the
floats, they are sometimes hung upon centres, and are so moved by suitable
131mechanism that they are always in a nearly vertical position when passing
through the water. Paddle-wheels constructed in this manner are termed
feathering wheels. They do not appear, however, to possess any great
advantage over those of the ordinary construction, except when the paddles
are deeply immersed in the water, and this result may be better understood
when we reflect that the actual path of the floats through the water is not
circular, as it would be if the vessel itself did not move; for all points of
the wheel describe peculiar curves called cycloids, which result from the
combination of the circular with the onward movement.
PLATE VIII.
THE “CLERMONT,” FROM A CONTEMPORARY DRAWING.
Fig. 59.—Casting Cylinder of a Marine Steam Engine.
The next figure, 60, exhibits a very common form of the screw propeller,
and shows the position which it occupies in the ship. The reader may not at
once understand how a comparatively small two-armed wheel revolving in a
plane perpendicular to the direction of the vessel’s motion is able to propel
the vessel forward. In order to understand the action of the propeller, he
should recall to mind the manner in which a screw-nail in a piece of wood
advances by a distance equal to its pitch at every turn. If he will conceive
a gigantic screw-nail to be attached to the vessel extending along the keel,—and
suppose for a moment that the water surrounding this screw is not
able to flow away from it, but that the screw works through the water as
the nail does in the wood,—he will have no difficulty in understanding that,
under such circumstances, if the screw were made to revolve, it would advance
and carry the vessel with it. The reader may now form an accurate
notion of the actual propeller by supposing the imaginary screw-nail to
have the thread so deeply cut that but little solid core is left in the centre,
132and supposing also that only a very short piece of the screw is used—say
the length of one revolution—and that this is placed in the dead-wood.
Such was the construction of the earlier screw-propellers, but now a still
shorter portion of the screw is used; for instead of a complete turn of the
thread, less than one-sixth is now the common construction. Such a strip
or segment of the screw-thread forms a blade, and two, three, four, or more
blades are attached radially to one common axis. The blades spring when
there are two from opposite points in the axis, and in other cases from
points on the same circle. The
blades of the propeller are cut
and carved into every variety of
shape according to the ideas of
the designer, but the fundamental
principle is the same in all
the forms. It need hardly be
said that the particles of the
water are by no means fixed like
those of the wood in which a
screw advances. But as the water
is not put in motion by the screw
without offering some resistance
by reason of its inertia, this resistance
reacting on the screw
operates in the same manner,
but not to the same extent, as the
wood in the other case. When
we know the pitch of the screw,
we can calculate what distance
the screw would be moved forward
in a given number of revolutions if it were working through a solid.
This distance is usually greater than the actual distance the ship is propelled,
but in some cases the vessel is urged through the water with a
greater velocity than if the screw were working in a solid nut. The shaft
which carries the screw extends from the stem to the centre of the ship
where the engines are placed, and it passes outward through a bearing lined
with wood, of which lignum vitæ is found to be the best kind, the lubricant
for this bearing being not oil but water. The screw would not have met
with the success it has attained but for this simple contrivance; for it was
found that with brass bearings a violent thumping action was soon produced
by the rapid rotation of the screw. The wearing action between the wood
and the iron is very slight, whereas brass bearings in this position quickly
wear and their adjustments become impaired. The screw-shaft is very
massive and is made in several lengths, which are supported in appropriate
bearings; there is also a special arrangement for receiving the thrust
of the shaft, for it is by this thrust received from the screw that the vessel
is propelled, and the strain must be distributed to some strong part of the
ship’s frame. There is usually also an arrangement by which the screw-shaft
can, when required, be disconnected from the engine, in order to
allow the screw to turn freely by the action of the water when the vessel is
under sail alone.
Fig. 60.—Screw Propeller.
A screw-propeller has one important advantage over paddle-wheels in
the following particular: whereas the paddle-wheels act with the best
effect when the wheel is immersed in the water to the depth of the lowest
133float, the efficiency of the screw when properly placed is not practically
altered by the depth of immersion. As the coals with which a steamer
starts for a long voyage are consumed, the immersion is decreased—hence
the paddle-wheels of such a steamer can never be immersed to the proper
extent throughout the voyage; they will be acting at a disadvantage during
the greater part of the voyage. Again, even when the immersion of the
vessel is such as to give the best advantage to the paddle-wheels, that advantage
is lost whenever a side-wind inclines the ship to one side, or whenever
by the action of the waves the immersion of the paddles is changed
by excess or defect. From all such causes of inefficiency arising from the
position of the vessel the screw-propeller is free. The reader will now
understand why paddle-wheel steamers are at the present day constructed
for inland waters only.
A great impulse was given to steam navigation, by the substitution of iron
for wood in the construction of ships. The weight of an iron ship is only
two-thirds that of a wooden ship of the same size. It must be remembered
that, though iron is many times heavier than wood, bulk for bulk, the required
strength is obtained by a much less quantity of the former. A young
reader might, perhaps, think that a wooden ship must float better than an
iron one; but the law of floating bodies is, that the part of the floating body
which is below the level of the water, takes up the space of exactly so much
water as would have the same weight as the floating body, or in fewer words,
a floating body displaces its own weight of water. Thus we see that an
iron ship, being lighter than a wooden one, must have more buoyancy. The
use of iron in ship-building was strenuously advocated by the late Sir W.
Fairbairn, and his practical knowledge of the material gave great authority
to his opinion. He pointed out that the strains to which ships are exposed
are of such a nature, that vessels should be made on much the same principles
as the built-up iron beams or girders of railway bridges. How
successfully these principles have been applied will be noticed in the case
of the Great Eastern. This ship, by far the largest vessel ever built, was
designed by Mr. Brunel, and was intended to carry mails and passengers
to India by the long sea route. The expectations of the promoters were
disappointed in regard to the speed of the vessel, which did not exceed 15
miles an hour; and no sooner had she gone to sea than she met with a
series of accidents, which appear, for a time, to have destroyed public confidence
in the vessel as a sea-going passenger ship. Some damage and
much consternation were produced on board by the explosion of a steam
jacket a few days after the launch. Then the huge ship encountered a
strong gale in Holyhead Harbour, and afterwards was disabled by a hurricane
in the Atlantic, in which her rudder and paddles were so damaged,
that she rolled about for several days at the mercy of the waves. At New
York she ran upon a rock, and the outer iron plates were stripped off the
bottom of the ship for a length of 80 ft. She was repaired and came home
safely; but the companies which owned her found themselves in financial
difficulties, and the big ship, which had cost half a million sterling, was
sold for only £25,000, or only about one-third of her value as old materials.
The misfortunes of the Great Eastern, and its failure as a commercial
speculation in the hands of its first proprietors, have been quoted as an
illustration of the ill luck, if it might be so called, which seems to have
attended several of the great works designed by the Brunels—for the
Thames Tunnel was, commercially, a failure; the Great Western Railway,
with its magnificent embankments, cuttings, and tunnels, has reverted to
134the narrow gauge, and therefore the extra expense of the large scale has
been financially thrown away; the Box Tunnel, a more timid engineer
would have avoided; and then there is the Great Eastern. It is, however,
equally remarkable that all these have been glorious and successful achievements
as engineering works, and the scientific merit of their designers
remains unimpaired by the merely accidental circumstance of their not
bringing large dividends to their shareholders. Nor is their value to the
world diminished by this circumstance, for the Brunels showed mankind
the way to accomplish designs which, perhaps, less gifted engineers would
never have had the boldness to propose. The Box Tunnel led the way to
other longer and longer tunnels, culminating in that of Mont Cenis; but
for the Thames Tunnel—once ranked as the eighth wonder of the world—we
should probably not have heard of the English Channel Tunnel—a
scheme which appears less audacious now than the other did then; if no
Great Eastern had existed, we should not now have had an Atlantic Telegraph.
Possibly this huge ship is but the precursor of others still larger,
and it is undoubtedly true that since its construction the ideas of naval
architects have been greatly enlarged, and the tendency is towards increased
size and speed in our steam-ships, whether for peace or war.
Fig. 61.—Section of Great Eastern Amidships.
Fig. 62.—The Great Eastern in course of Construction.
The accidents which had happened to the ship had not, however, materially
damaged either the hull or the machinery; and the Great Eastern was
refitted, and afterwards employed in a service for which she had not been
designed, but which no other vessel could have attempted. This was the
work of carrying and laying the whole length of the Atlantic Telegraph
Cable of 1865, of which 2,600 miles were shipped on board in enormous
tanks, that with the contents weighed upwards of 5,000 tons. The ship has
since been constantly engaged in similar operations.[1] The Great Eastern
is six times the size of our largest line-of-battle ships, and about seven
times as large as the splendid steamers of the Cunard line, which run
between Liverpool and New York. She has three times the steam power
of the largest of these Atlantic steamers, and could carry twenty times as
135many passengers, with coal for forty days’ consumption instead of fifteen.
Her length is 692 ft.; width, 83 ft.; depth, 60 ft.; tonnage, 24,000 tons;
draught of water when unloaded, 20 ft.; when loaded, 30 ft.; and a promenade
round her decks would be a walk of more than a quarter of a mile.
The vessel is built on the cellular plan to 3 ft. above the water-line; that
is, there is an inner and an outer hull, each of iron plates ¾ in. thick, placed
2 ft. 10 in. apart, with ribs every 6 ft., and united by transverse plates, so
that in place of the ribs of wooden ships, the hull is, as it were, built up of
curved cellular beams of wrought iron. The ship is divided longitudinally by
two vertical partitions or bulkheads of wrought iron, ½ in. thick. These are
350 ft. long and 60 ft. high, and are crossed at intervals by transverse bulkheads,
in such a manner that the ship is divided into nineteen compartments,
of which twelve are completely water-tight, and the rest nearly so.
The diagram (Fig. 61) represents a transverse section, and shows the cellular
construction below the water-line. The strength and safety of the vessel
are thus amply provided for. The latter quality was proved in the accident
to the ship at New York; and the former was shown at the launch, for
when the vessel stuck, and for two months could not be moved, it was found
that, although one-quarter of the ship’s length was unsupported, it exhibited
no deflection, or rather the amount of deflection was imperceptible. Fig. 62
is from a photograph taken during the building of the ship, and Fig. 63
shows the hull when completed and nearly ready for launching, while the
vignette at the head of the chapter exhibits the big ship at anchor when
completely equipped. The paddle-wheels are 56 ft. in diameter, and are
136turned by four steam engines, each having a cylinder 6 ft. 2 in. in diameter,
and 14 ft. in length. The vessel is also provided with a four-bladed screw-propeller
of 24 ft. diameter, driven by another engine having four cylinders,
six boilers, and seventy-two furnaces. The total actual power of the engines
is more than that of 8,000 horses, and the vessel could carry coals enough
to take her round the world—a capability which was the object of her
enormous size. The vessel as originally constructed contained accommodation
for 800 first-class passengers, 2,000 second class, and 1,200 third
class—that is, for 4,000 passengers in all. The principal saloon was 100 ft.
long, 36 ft. wide, and 13 ft. high. Each of her ten boilers weighs 50 tons,
and when all are in action, 12 tons of coal are burnt every hour, and the
total displacement of the vessel laden with coal is 22,500 tons.
The use of steam power in navigation has increased at an amazing rate.
Between 1850 and 1860 the tonnage of the steam shipping entering the
port of London increased three-fold, and every reader knows that there
are many fleets of fine steamers plying to ports of the United Kingdom.
There are, for example, the splendid Atlantic steamers, some of which
almost daily enter or leave Liverpool, and the well-appointed ships belonging
to the Peninsular and Oriental Company. The steamers on the Holyhead
and Kingston line may be taken as good examples of first-class passenger
ships. These are paddle-wheel boats, and are constructed entirely
of iron, with the exception of the deck and cabin fittings. Taking one of
these as a type of the rest, we may note the following particulars: the vessel
is 334 ft. long, the diameter of the paddle-wheels is 31 ft., and each has
fourteen floats, which are 12 ft. long and 4 ft. 4 in. wide. The cylinders of
the engines are 8 ft. 2 in. in diameter, and 6 ft. 6 in. long. The ship cost
137about £75,000. The average passage between the two ports—a distance
of 65½ miles—occupies 3 hours 52 minutes, and at the measured mile the
vessel attained the speed of 20·811 miles per hour. As an example of the
magnificent vessels owned by the Cunard Company, we shall give now a
few figures relating to one of their largest steam-ships, the Persia, launched
in 1858, and built by Mr. N. Napier, of Glasgow, for the company, to carry
mails and passengers between Liverpool and New York. Her length is
389 ft., and her breadth 45 ft. She is a paddle-wheel steamer, with engines
of 850 horse-power, having cylinders 100 in. in diameter with a stroke of
10 ft. The paddle-wheels are 38 ft. 6 in. in diameter, and each has twenty-eight
floats, 10 ft. 8 in. long and 2 ft. wide. The Persia carries 1,200 tons
of coal, and displaces about 5,400 tons of water.
Fig. 64.—Comparative Sizes of Steamships.
1838, Great Western; 1844, Great Britain; 1856, Persia; 1858, Great Eastern.
A, Section amidships of Great Eastern; B, The same of Great Western. Both on the same scale, but on a larger one than their profiles.
A velocity of twenty-six miles per hour appears to be about the highest
yet attained by a steamer.[2] This is probably near the limit beyond which
the speed cannot be increased to any useful purpose. The resistance offered
by water to a vessel moving through it increases more rapidly than the
velocity. Thus, if a vessel were made to move through the water by being
pulled with a rope, there would be a certain strain upon the rope when the
vessel was dragged, say, at the rate of five miles an hour. If we desired the
vessel to move at double the speed, the strain on the rope must be increased
four-fold. To increase the velocity to fifteen miles per hour, we should
have to pull the vessel with nine times the original force. This is expressed
by saying that the resistance varies as the square of the velocity. Hence,
to double the speed, the impelling force must be quadrupled, and as that
force is exerted through twice the distance in the same time, an engine
would be required of eight times the power—or, in other words, the power
138of the engine must be increased in proportion to the cube of the velocity;
so that to propel a boat at the rate of 15 miles an hour would require
engines twenty-seven times more powerful than those which would suffice
to propel it at the rate of five miles an hour.
2. This has now (1895) been far surpassed.—Vide infra.
The actual speed attained by steam-ships with engines of a given power
and a given section amidships will depend greatly upon the shape of the
vessel. When the bow is sharp, the water displaced is more gradually and
slowly moved aside, and therefore does not offer nearly so much resistance
as in the opposite case; but the greater part of the power required to urge
the vessel forward is employed in overcoming a resistance which in some
degree resembles friction between the bottom of the vessel and the water.
The wonderful progress which has, in a comparatively short time, taken
place in the power and size of steam-vessels, cannot be better brought
home to the reader than by a glance at Fig. 64, which gives the profiles of
four steamships, drawn on one and the same scale, thus showing the relative
lengths and depths of those vessels, each of which was the largest
ship afloat at the date which is marked below it, and the whole period includes
only the brief space of twenty years!—for this, surely, is a brief
space in the history of such an art as navigation. All these ships have
been named in the course of this article, but in the following table a few
particulars concerning each are brought together for the sake of comparing
the figures:
Date.
Name.
Propulsion.
Length.
Breadth.
1838
Great Western
Paddles
236 ft.
36 ft.
1844
Great Britain
Screw
322 ft.
51 ft.
1856
Persia
Paddles
390 ft.
45 ft.
1858
Great Eastern
Screw and paddles
690 ft.
83 ft.
Fig. 65.—The s.s. City of Rome.
Several passenger ocean-going steamships have been built since the
Persia, of still greater dimensions, and of higher engine power. These
139have generally been surpassed in late years by some splendid Atlantic
liners, such as the sister vessels owned by the International Navigation
Co., and now named respectively the New York and the Paris. The City
of Rome, launched in 1881 by the Barrow Steamship Co., is little inferior
in length to the Great Eastern, although the tonnage is only about one-third.
The City of Rome is 560 ft. long, 52 ft. wide, and 37 ft. deep. Her
engines are capable of working up to 10,000 indicated horse-power. Fig.
65 is a sketch of this ship, and shows that she carries four masts and three
funnels. The main shaft measures more than 2 ft. across, and the screw-propeller
is 24 ft. in diameter. She has accommodation for 1,500 passengers,
and is fitted with all the conveniences and luxuries of a well-appointed
hotel. The International Navigation Co.’s ship Paris, has made the
passage across the Atlantic in less than six days, and appears to be the
fastest vessel in the transatlantic service. In August, 1889, she made
the run from shore to shore in 5 days, 22 hours, 38 minutes.
The extraordinary increase in the speed of steamships that has been
effected within the last few years depends mainly upon the improvements
that have latterly been made in the marine engine—a machine of which
we have been unable to give an account, because its details are too
numerous and complicated to be followed out by the general reader.
Suffice it to say, that the use of higher steam pressures with compound
expansion (p. 18), condensers which admit of the same fresh water
being used in the boilers over and over again, and better furnace
arrangements, are among the more important of these improvements.
But not only have the limits of practicable speed been enlarged, but a
greater economy of fuel for the work done has been attained; the result
being that ocean carriage is now cheaper than ever. The outcome of
this will not cease with simply a greatly extended steam navigation, but
appears destined ultimately to produce effects on the world at large
comparable in range and magnitude with those that may be traced to the
use of the steam engine itself since its first invention.
Among the curiosities of steamboat construction may be mentioned a
remarkable ship which was built a few years ago for carrying passengers
across the English Channel without the unpleasant rolling experienced in
the ordinary steamboats. The vessel, which received the name of the
Castalia, was designed by Captain Dicey, who formerly held an official
position at the Port of Calcutta. His Indian experience furnished him
with the first suggestion of the new ship in the device which is adopted
there for steadying boats in the heavy surf. The plan is to attach a log
of timber to the ends of two outriggers, which project some distance from
the side of the vessel; or sometimes two canoes, a certain distance apart,
are connected together. Some of these Indian boats will ride steadily in
a swell that will cause large steamers to roll heavily. Improving on this
hint, Captain Dicey built a vessel with two hulls, each of which acted as
an outrigger to the other. Or, perhaps, the Castalia may be described as
a flat-bottomed vessel with the middle part of the bottom raised out of the
water throughout the entire length, so that the section amidships had a
form like this—
The two hulls were connected by
what we may term “girders,” which extended
completely across their sections, forming
transverse partitions or bulkheads, and these
girders were strongly framed together, so as to
form rigid triangles. These united the two hulls so completely, that
140there was not any danger of the vessel being strained in a sea-way. The
decks were also formed of iron, although covered with wood, so that the
whole vessel really formed a box girder of enormous section.
Fig. 66.—The Castalia in Dover Harbour.
The reason why the steamers which until lately ran between Dover and
Calais, Folkestone and Boulogne, and other Channel ports, were so small,
was because the harbours on either side could not receive vessels with such
a draught as the fine steamers, for example, which run on the Holyhead
and Kingston line. Now, the Castalia drew only 6 ft. of water, or 1 ft. 6 in.
less than the small Channel steamers, and would, therefore, be able to enter
the French ports at all states of the tide. Yet the extent of the deck space
was equalled in few passenger ships afloat, except the Great Eastern and
some of the Atlantic steamers. The vessel was 290 ft. in length, with an
extreme breadth of 60 ft. The four spacious and elegantly-fitted saloons—two
of which were 60 ft. by 36 ft., and two 28 ft. by 26 ft.—and the roomy
cabins, retiring rooms, and lavatories, were the greatest possible contrast
to the “cribbed, cabined, and confined” accommodation of the ordinary
Channel steamers. There were also a kitchen and all requisites for supplying
dinners, luncheons, etc., on board. But besides the above-named
saloons and cabins, there was a grand saloon, which was 160 ft. long and
60 ft. wide; and the roof of this formed a magnificent promenade 14 ft.
above the level of the sea. There was comfortable accommodation in the
vessel for more than 1,000 passengers.
The inner sides of the hulls were not curved like the outside, but were
straight, with a space between them of 35 ft. wide, and the hulls were each
20 ft. in breadth, and somewhat more in depth. There were two paddle-wheels,
141placed abreast of each other in the water-way between the two
hulls, and each of these contained boilers and powerful engines. The designers
of this vessel calculated that she would attain a speed of 14¾ knots
per hour, but this result failed to be realized. Probably there were no
data for the effect of paddles working in a confined water-space. The
position of the paddles is otherwise an advantage, as it leaves the sides of
the vessel free and unobstructed. The ship had the same form at each
end, so it could move equally well in either direction. There were rudders
at both ends, and the steering qualities of the ship were good. Although
the speed of the Castalia was below that intended, the vessel was a success
as regards steadiness, for the rolling and pitching were very greatly
reduced, and the miseries and inconveniences of the Channel passage
obviated.
Fig. 67.—The Castalia in Dover Harbour—End View.
The Castalia is represented in Figs. 66 and 67. She was constructed
by the Thames Iron Shipbuilding Co., and launched in June, 1874, but
after she had been tried at sea, it was found necessary to fit her with improved
boilers, and this caused a delay in placing the vessel on her
station.
The Castalia proved a failure in point of speed, and she was soon replaced
by another and more powerful vessel constructed on the same
general plan, and named the Calais-Douvres. But this twin-ship again
failed to answer expectations, and as the harbour on the French shore
was meanwhile deepened and improved, new and very fine paddle-wheel
142boats, named the Invicta, Victoria, and Empress have been placed on the
service. As the latter boat, at least, has steamed from Dover to Calais,
nearly twenty-six miles, under the hour, there is nothing more to be
desired in point of speed. A fourth vessel is to take the place of the twin-ship,
Calais-Douvres, and will receive the same name.
Fig. 68.—Bessemer Steamer.
Another very novel and curious invention connected with steam navigation
was the steamer which Mr. Bessemer built at Hull in 1874. This
invention also was to abolish all the unpleasant sensations which landsmen
are apt to experience in a sea voyage, by effectually removing the
cause of the distressing mal de mer. The ship was built for plying
between the shores of France and England, and the method by which he
purposed to carry passengers over the restless sea which separates us
from our Gallic neighbours was bold and ingenious. He designed a
spacious saloon, which, instead of partaking of the rolling and tossing of
the ship, was to be maintained in an absolutely level position. The saloon
was suspended on pivots, much in the same way as a mariner’s compass
is suspended; and by an application of hydraulic power it was intended to
counteract the motion of the ship and maintain the swinging saloon perfectly
horizontal. It was originally proposed that the movements should
be regulated by a man stationed for that purpose, where he could work
the levers for bringing the machinery into action, so as to preserve the
saloon in the required position. This plan was, however, improved upon,
and the adjustments made automatic. It may be well to mention that it
is a mistake to suppose that anything freely suspended, like a pendulum,
on board a ship rolling with the waves, will hang vertically. If, however,
143we cause a heavy disc to spin very rapidly, say in a horizontal plane, the
disc cannot be moved out of the horizontal plane without the application
of some force. A very well-made disc may be made to rotate for hours,
and would, by preserving its original plane of rotation, even show the
effect of the earth’s diurnal motion. Mr. Bessemer designed such a gyroscope
to move the valves of his hydraulic apparatus, and so to keep his
swinging saloon as persistently horizontal as the gyroscope itself. Mr.
Bessemer’s ship was 350 ft. long, and each end, for a distance of 48 ft., was
only about 4 ft. from the line of floating. Above the low ends a breastwork
was raised, about 8 ft. high, and 254 ft. long. In the centre, and occupying
the space of 90 ft., was the swinging saloon intended for first-class
passengers. At either end of this apartment were the engines and boilers.
The engines were oscillating and expansive, working up to 4,600 horse-power,
which could be increased to 5,000. There were two pairs of
engines, one set at either end of the ship, and each having two cylinders
of 80 in. in diameter, and a stroke of 5 ft., working with steam of 30 lbs.
pressure per square inch, supplied from four box-shaped boilers, each
boiler having four large furnaces. The paddle-wheels, of which there
were a pair on either side of the vessel, were 27 ft. 10 in. in diameter outside
the outer ring, and each wheel has twelve feathering floats. The
leading pair of wheels, when working at full speed, were to make thirty-two
revolutions per minute, and the following pair of wheels move faster.
Entrance into the Bessemer saloon was gained by two broad staircases
leading to one landing, and a flexible passage from this point to the saloon.
The saloon rested on four steel gudgeons, one at each end, and two close
together near the middle. These were not only to support the saloon,
but also to convey the water to the hydraulic engines, by which the saloon
was to be kept steady. For this purpose the after one was made hollow,
and connected with the water mains from powerful engines, and also with
a supply-pipe leading to a central valve-box, by means of which the two
hydraulic cylinders on either side were supplied with water. Between
the two middle gudgeons, a gyroscope, worked by a small turbine, filled
with water from one of the gudgeons, enabled Mr. Bessemer to dispense
with the services of a man, and thus completed his scheme of a steady
saloon, by making the machinery completely automatic. The saloon was
70 ft. long, 35 ft. wide, and 20 ft. high. The Bessemer ship proved to be
a total failure, and never went to sea as a passenger boat.
On board of some modern war-ships where speed is essential, and
where the engines are driven at a very great number of revolutions per
minute, as in the case of torpedo-boat catchers, the vibration throughout
the whole of the vessel becomes extremely trying, not only for the nerves
of the crew, but for the security of the structure itself. The cause of this
vibration and consequent strain and loss of power is not far to seek. The
cylinders of marine engines are always of a large diameter, 6 feet, 8 feet,
or even more sometimes, and the pistons and piston-rods are necessarily
of great strength and corresponding weight. Now, at every half revolution
of the engines, this heavy mass of piston and piston-rod, though
moving at an exceedingly high speed in the middle of the stroke, has to
be brought to a standstill, and an equal velocity in the opposite direction
imparted to it. A large portion of the power is therefore uselessly expended
in stopping a great moving mass, and reversing its motion. All
the force required to do this reacts on the vessel’s frame. Many attempts
have been made to construct rotatory steam-engines, and some hundreds
144of patents taken out for such inventions, which in general have a piston
revolving about a shaft; but the great friction, and consequent liability to
wear out, have prevented their practical use.
Lately, a method of using steam on the principle embodied in the water
turbine has been developed, and within the last six or seven years has
found successful application in propelling electro-dynamos at very high
speeds. In the steam turbine there are no pistons, piston-rods, or other
reciprocating parts, the effect depending on the same kind of reaction that
is taken advantage of in the water turbine (which has a high efficiency in
giving out a large proportion of energy), and the power is applied with
smoothness and an entire absence of the oscillations that would shake to
pieces any vessel that an ordinary steam-engine could propel at the same
rate.
The advantages of the steam turbine have been proved by the performances
of a small experimental vessel lately built at Newcastle, and appropriately
named the Turbinia. She is only 100 feet in length, and 9
feet in breadth, with a displacement of some 44 tons. Now the highest
record speed for any vessel of that size is 24 knots per hour; but the
Turbinia, in a heavy sea, showed, at a measured mile, the speed of 32¾
knots, which is believed to be greater than that of any craft now afloat,
being nearly 37¾ miles an hour, or equal to that of an ordinary railway
train. Besides that, it has been found by experiment, that an arrangement
of the blades of the screw propeller more suitable to high velocities
will enable a still greater speed to be obtained. The weight of the turbine
engines of this vessel is only 3 tons, 13 cwts., and the whole weight of the
machinery, including boilers and condensers, is only 22 tons, with an indicated
H.P. of 1576, and a steam consumption of but 16 lbs. per hour.
The weight of the turbine is only one-fifth of that of marine engines of
equal power; the space occupied is smaller; the initial cost is less; not
so much superintendence is required; the charges of maintenance are
diminished; reduced dimensions of propeller and shaft suffice; vibration
is eliminated; speed is increased; and greater economy of fuel is secured.
The chapter on “Steam Navigation,” in the foregoing pages, has dealt
mainly with the progress of the ocean-going steam-ship, from the
establishment of regular transatlantic services down to the building of the
splendid liners, the New York and the Paris, and we have recorded, in
addition, the performances of the pair of hitherto unsurpassed sister ships,
the Campania and the Lucania. The importance and interest attaching
to steam navigation is, however, by no means confined to ocean-going
vessels, and the chapter demands a supplementary notice of the great
developments of the steam-ship in other parts of the world than Britain,
more particularly where great rivers, navigable for hundreds of miles,
and lakes, spreading their waters over vast areas, present conditions of
traffic and opportunities for adaptation to an extent that could not be
required within the range of Britain or British oceanic lines.
PLATE IX.
THE “MARY POWELL.”
145If the reader will cast his eye on the map of the United States, he will
see towards the northern boundary a great fresh-water system, comprising
five enormous lakes, the least of which is nearly two hundred, and the
largest nearly three hundred miles in length, in all presenting a total area
greater by far than that of England and Scotland together thrice told. This
lake system has a line of coast to be reckoned only by thousands of miles,
and for a long time an enormous traffic has been carried across its waters
by sailing vessels of all kinds, two- or three-masted schooners, brigs, and
other craft, carrying wood, stone, lime, and other commodities. On the
map, the position of the Detroit River, which leads from the southern
extremity of Lake Huron to Lake Erie, will readily be recognised, and
this strait, which is in the only line of transport from the three great
upper lakes, formerly presented all the picturesqueness that crowds of
boats of every build could impart. Especially was this the case at
Amherstburg, its southern extremity, where sometimes a northern wind
would make the passage impracticable for several days in succession, and
a fleet of a hundred or two hundred sailing vessels would collect to await
the opportunity of a favouring breeze in order to carry them against the
current to Port Huron. Then, taking advantage of the right moment,
they would set their sails, and in a compact body move slowly up the
strait. This was not quick enough to meet the traffic, and, before long,
larger vessels were built, which were towed up and down the Detroit by
steam-tugs. The next step of replacing sailing ships by steam-vessels was
not long in following, and though there still exist fine specimens of sailing
craft on the lakes, their day may be said to be over. The navigation of
these lakes, before the extensive development of the railway systems near
their shores, comprised a large passenger traffic, which was carried on by
big paddle-wheel steamers, and at the time of the great westward set of
emigration to Michigan, Wisconsin, and Minnesota, these steamers were
crowded to their utmost capacity. The great improvement which in
recent years has become possible for passenger steamers in speed, cabin
accommodation, and other particulars, above all, the growth of great
cities on the shores, the progress of the territories adjoining the lake
system, and other circumstances, are now combining to renew the passenger
traffic on a larger scale than ever. “Fifteen millions of people,”
says Mr. H. A. Griffin, the Secretary of the Cleveland Board of Control
(Engineering Magazine, iv., 819), “now live upon the shore lines of the
lakes, or within six hours’ travel by rail, and nearly all of that population
is south of the United States boundary line. The territory directly
tributary to the lakes, north and south of the line, is capable of easily
maintaining a population of 100,000,000.... It does not require a very
lively imagination to foresee the Great Lakes surrounded by the most
prosperous and progressive people on earth, and crossed and recrossed
by scores of lines of passenger steam-ships, in addition to a still greater
number of freight lines.” The number of first-class passenger steamers
already launched or on the stocks is an indication that the revival of
passenger traffic will not lag or be delayed.
The unique conditions and requirements of this lacustrine traffic were
bound to lead to types of vessels differing in many respects from the
steam-ships to be seen in the harbours of Great Britain. The introduction
of iron shipbuilding gave a great impetus to the construction of the
lake steamers, for vessels of more than 3,000 tons could be built with a
comparatively shallow draught of water (15½ feet), which was one of the
146necessities of the situation. As far back as 1872, iron shipbuilding had
been fully established at Cleveland and Detroit, and at the latter place
scores of splendid steel steam-ships have been turned out. The Cleveland
builders have not been far behind, and Buffalo, Milwaukee, Chicago, and
other places, have followed suit. At the beginning of 1893, there were on
the lakes more than fifty vessels of over 2,000 tons each, while the total
number of steam vessels of all kinds was considerably over 1,600, and
sailing vessels with steam-tugs counted over 2,000. The tonnage of the
ships on the lakes has been estimated at about 36 per cent. of the whole
mercantile marine of the United States, and it is said that 40,000 men are
employed upon the vessels. The total freight passing Detroit in 1892
was calculated to exceed 34,000,000 tons, an amount greater than the
whole foreign and coasting trade of the port of London. There are more
than thirty shipbuilding concerns on the lakes, and some of them possess
large dry docks of their own; but there are also independent companies
owning dry docks of great size. Some of these shipbuilding establishments
have turned out steel ocean-going tugs, paddle and screw passenger
steamers, cargo-carrying boats, vessels for carrying railway trains
across the Detroit river, etc., etc.
Fig. 68a.—A Whaleback Steamer, No. 85, Built at West Superior, Wisconsin.
The extent and importance which steam navigation has attained in a
definite region have been indicated in the preceding paragraphs; but an
attempt to show by illustration and description the several characteristic
forms the steam-ship has now assumed in these lacustrine waters would
carry us far beyond our allotted limits. The steam vessels now on the
lakes are almost exclusively actuated by screw-propellers, whether they
are passenger or freight boats. The boilers and engines are near the stern,
and the hulls are usually of great length; in fact, some of these steamboats
will compare in dimensions with the Persia, which was the transatlantic
marvel about the year 1857. (See p. 137.) Such is the Mariposa,
launched in 1892, which is 350 feet long and 45 feet broad, carrying 3,800
net tons, with a draught of only 15½ feet. There are others, 380 feet long,
with engines of 7,000 horse-power, steaming at 20 miles an hour, and providing
147ample accommodation for 600 passengers. The newest and most
novel type of steam-ship on the lakes is the “whaleback.” The celerity
with which ships of this kind have been constructed on occasion is
perfectly marvellous. One of them, named the Christopher Columbus,
designed to carry passengers to and from the World’s Fair at Chicago in
1893, was launched in fifty-six days after the keel had been laid, yet it
was a ship intended to carry 5,000 passengers, having a length over all
of 362 feet, breadth 42 feet, depth 24 feet. The “whaleback” steamers
are designed to give the greatest carrying capacity with a given
draught of water, and all the structures usually fitted to the upper
deck of a steamer are in them replaced by the plain curved and
closed deck, over which, when the vessel is in a storm, waves may
sweep harmlessly, thus avoiding the shocks received by ships with high
sides.
The river steam-boat was, as we have seen, nearly coeval with the nineteenth
century, and although its practicability was first demonstrated in
British waters, regular steam navigation was not established until a few
years afterwards, when, in 1807, Robert Fulton placed on the River
Hudson its first steam-boat. To this others were soon added, so that in
1813 there were six steam-boats regularly plying on the Hudson before a
single one ran for hire on the Thames. An article by Mr. Samuel Ward
Stanton, in a recent number of The Engineering Magazine, gives a very
full account of the Hudson River steam-boats from the beginning down
to 1894, and to this article we are mainly indebted for the details we are
about to give.
The Hudson River washes the western shore of Manhattan Island, on
which stands by far the greater part of the city of New York, with its
vast population. The river is here straight, and has a nearly uniform
width of one mile; at New York it is commonly called the North River,
because of the direction of its course, for it descends from almost the due
north. It is not one of the great rivers of the United States as regards
length or extent of navigation; not, e.g., like the Mississippi and the
Missouri, which are ascended by steam-boats to thousands of miles above
their mouths; but it has one of the world’s great capitals on its shores,
and at the quays, which occupy both its banks to the number of eighty or
more, may be seen in multitudes some of the finest ocean-going steamships,
trading to every considerable port in the world. The North River
separates New York from what are practically the populous suburbs of
Jersey City and Hoboken, though these are controlled by their own
municipalities.
It was on the River Hudson that steam navigation was inaugurated
by Fulton with a vessel which was 133 feet long, 18 feet broad, and
7 feet deep, and was named the Clermont. The speed attained was but
five miles an hour. The first trip was made on the 7th August, 1807, to
Albany, 150 miles up the river from New York, with twenty-four passengers
on board, and the new kind of locomotion was so well patronised
that during the following winter, when the Hudson navigation had to be
suspended on account of the ice, it was considered expedient to enlarge
the capacity of the boat by adding both to her length and width; at the
same time her name was changed to The North River, and she plied
regularly for several seasons afterwards. Her speed down the river with
the current was evidently greater than that of the first trip up the river,
for on 9th November, 1809, the New York Evening Post announced that
148“The North River steam-boat arrived this afternoon in twenty-seven and
a half hours from Albany, with sixty passengers.”
The paddle-wheels were of a primitive form, and as they were unprovided
with paddle-boxes, the arrangement had the appearance of a great undershot
mill-wheel on each side of the boat, above the deck of which was
placed the steam-engine, a position it has retained in all these river-boats,
in which a huge, rhombus-shaped beam, oscillating high above the deck,
is a conspicuous feature. Another boat of much larger dimensions was
built the following year, having a tonnage of nearly 300, and from that
time there has been a more or less regular increase in the sizes of the
vessels, until in 1866 a tonnage of nearly 3,000 was reached. In 1817 a
vessel called the Livingstone was launched, which was able to go up to
Albany in eighteen hours. In 1823 was launched the James Kent, a
novel feature in which vessel was the boiler made of copper, and weighing
upwards of 30 tons. It was so planned that if it happened to burst, the
hot water would be carried through the bottom of the vessel by tubes or
hollow pillars. From this it appears that considerable apprehension
existed as to the liability of the boilers exploding. We are told that the
cost of the copper boiler was in this case nearly one-third of that of the
whole vessel. The cabins are described as having been very handsomely
fitted up, and the speed was such that fourteen hours sufficed for the trip
up river to Albany. Many fine boats were placed on the river during the
twenty following years, and these were marked by various improvements,
as when, in 1840, anthracite coal was for the first time substituted for
wood as the fuel for the furnaces, with the effect of reducing the cost of
this item to one-half. Then, in 1844, iron began to be used for constructing
the hulls, and a few years afterwards, steamers having a speed of
twenty miles an hour and over, became quite common. In 1865, and
again in the eighties, some four screw-propeller boats were built; but
this type does not appear to have found much favour on the Hudson, for
the large paddle-wheels and the single or double beam, working high
above the deck, have continued the almost universal form of construction.
A very popular and famous boat was placed on the Hudson in 1861. This
was the Mary Powell, called the “Queen of the Hudson,” which, although
a boat of moderate tonnage (983), was able on occasion to steam at the
rate of twenty-five miles an hour. This vessel was placed on the line
between New York and Rondont, and was still running in 1894.
One of the most modern and most elegant boats on the Hudson is
the New York, launched in 1887, and declared by Mr. Stanton to be
one of the finest river steam-boats in the world, well arranged, and
beautifully finished and furnished. She is built on fine lines, is 311 feet
long, 40 feet broad, and with a tonnage of 1,552, draws only 12¼ feet of
water. She can steam at twenty miles an hour, and is placed on one
of the New York and Albany lines. Throughout the summer there are
both day and night boats for Albany, and the latter especially are of
great size, three stories high, and provided with saloons, state-rooms, and,
in fact, all the accommodation of a luxurious first-class hotel. The
vessels named in this notice include but a few of the splendid boats that
ply on the River Hudson, and, in respect of their numbers, speed, and
comfort, it may safely be asserted that they cannot be equalled on any
other river in the world.
PLATE X.
THE “NEW YORK.”
149
Fig. 69.—H.M.S. Devastation in Queenstown Harbour.
SHIPS OF WAR.
“Take it all in all, a ship of the line is the most honourable thing that
man, as a gregarious animal, has ever produced. By himself, unhelped,
he can do better things than ships of the line; he can make poems,
and pictures, and other such concentrations of what is best in him. But as a
being living in flocks, and hammering out with alternate strokes and mutual
agreement, what is necessary for him in those flocks to get or produce, the
ship of the line is his first work. Into that he has put as much of his
human patience, common sense, forethought, experimental philosophy, self-control,
habits of order and obedience, thoroughly wrought hand-work,
defiance of brute elements, careless courage, careful patriotism, and calm
expectation of the judgment of God, as can well be put into a space of
300 ft. long by 80 ft. broad. And I am thankful to have lived in an age
when I could see this thing so done.” So wrote Mr. Ruskin about forty
years ago, referring, of course, to the old wooden line-of-battle ships. It
may be doubted whether he would have written thus enthusiastically about
so unpicturesque an object as the Glatton, just as it may be doubted whether
the armour-plated steamers will attain the same celebrity in romance and in
150verse as the old frigates with their “wooden walls.” Certain it is that the
patience, forethought, experimental philosophy, thoroughly wrought hand-work,
careful patriotism, and other good qualities which Mr. Ruskin saw
in the wooden frigates, are not the less displayed in the new ironclads.
Floating batteries, plated with iron, were employed in the Crimean War
at the instigation of the French Emperor. About the same time the question
of protecting ships of war by some kind of defensive armour was
forced upon the attention of maritime powers, by the great strides with
which the improvements in artillery were advancing; for the new guns
could hurl projectiles capable of penetrating, with the greatest ease, any
wooden ship afloat. The French Government took the initiative by constructing
La Gloire, a timber-framed ship, covered with an armour of rolled
iron plates, 4½ in. thick. The British Admiralty quickly followed with the
Warrior, a frigate similar in shape to the wooden frigates, but built on
an iron frame, with armour composed of plates 4½ in. thick, backed by 18 in.
of solid teak-wood, and provided with an inner skin of iron. The Warrior
was 380 ft. long, but only 213 ft. of this length was armoured. The defensive
armour carried by the Warrior, and the ironclads constructed immediately
afterwards, was quite capable of resisting the impact of the 68 lb. shot,
which was at that time the heaviest projectile that could be thrown by
naval guns. But to the increasing power of the new artillery it soon became
necessary to oppose increased thickness of iron plates. The earlier ironclads
carried a considerable number of guns, which could, however, deliver
only a broadside fire, that is, the shots could, for the most part, be sent
only in a direction at right angles to the ship’s length, or nearly so. But
in the more recently built ironclads there are very few guns, which are,
however, six times the weight of the old sixty-eight pounders, and are capable
of hurling projectiles of enormous weight. The ships built after the
Warrior were completely protected by iron plates, and the thickness of the
plates has been increased from time to time, with a view of resisting the
increased power which has been progressively given to naval guns. A
contest, not yet terminated, has been going on between the artillerist and
the ship-builder; the one endeavouring to make his guns capable of penetrating
with their shot the strongest defensive armour of the ships, the
other adding inch after inch to the thickness of his plates, in order, if possible,
to render his ship invulnerable.
Fig. 70.—Section of H.M.S. Hercules.
One of the finest of the large ironclads is the Hercules, of which a section
amidships is presented on the next page. This ship is 325 ft. in length,
and 59 ft. in breadth, and is fitted with very powerful engines which will
work up to 8,529 indicated horse-power. The tonnage is 5,226; weight of
hull, 4,022 tons; weight of the armour and its backing, 1,690 tons; weight
of engines, boilers, and coals, 1,826 tons; total with equipment and armament,
8,676 tons. Although the Hercules carries this enormous weight of
armour and armament, her speed is very great, excelling, in fact, that of
any merchant steamer afloat, for she can steam at the rate of nearly 17
miles an hour. She also possesses, in a remarkable degree, the property
which naval men call handiness; that is, she can be quickly turned round
in a comparatively small space. The handiness of a steamer is tested by
causing her to steam at full speed with the helm hard over, when the vessel
will describe a circle. The smaller the diameter of that circle, and the
shorter the time required to complete it, the better will the vessel execute
the movements required in naval tactics. Comparing the performances of
the Warrior and the Hercules, we find that the smallest circle the former
152can describe is 1,050 yards in diameter, and requires nine minutes for its
completion, whereas the latter can steam round a circle of only 560 yards
diameter in four minutes. The section (Fig. 70) shows that, like the Great
Eastern, the Hercules is constructed with a double hull, so that she would
be safe, even in the event of such an accident as actually occurred to the
Great Eastern, when a hole was made by the stripping off of her bottom
plates, 80 ft. long and 5 ft. wide. The defensive armour of the Hercules is,
it will be observed, greatly strengthened near the water-line, where damage
to the ship’s side would be most fatal. The outer iron plates are here 9 in.
thick, while in other parts the thickness is 8 in., and in the less important
positions 6 in. The whole of the hull is, however, completely protected
above the water-line, and the iron plates are backed up by solid teak-wood
for a thickness of from 10 in. to 12 in. The teak is placed between girders,
which are attached to another iron plating 1½ in. thick, supported by girders
2 ft. apart. The spaces between these girders are also filled with teak, and
the whole is lined with an inner skin of iron plating, ¾ in. thick. The belt
along the water-line has thus altogether 11¼ in. of iron, of which 9 in. are in
one thickness, and this part is, moreover, backed by additional layers of
teak, as shown in the section; so that, besides the 11¼ in. of iron, the ship’s
side has here 3 ft. 8 in. total thickness of solid teak-wood. The deck is also
covered with iron plates, to protect the vessel from vertical fire. The
Hercules carries eight 18–ton guns as her central battery, and two 12–ton
guns in her bow and stern: these guns are rifled, and each of the larger
ones is capable of throwing a shot weighing 400 lbs. The guns can be
trained so as to fire within 15° of the direction of the keel; for near the
ends of the central battery the ports are indented, and the guns are mounted
on Scott’s carriages, in such a manner that any gun-slide can be run on to
a small turn-table, and shunted to another port, just as a railway-carriage
is shunted from one line to another. Targets for artillery practice were
built so as to represent the construction of the side of the Hercules, and
it was found, as the result of many experiments, that the vessel could not
be penetrated by the 600 lb. shot from an Armstrong gun, fired at a distance
of 700 yds. The production of such iron plates, and those of even greater
thickness which have since been used, forms a striking example of the skill
with which iron is worked. These plates are made by rolling, and it will
be understood that the machinery used in their formation must be of the
most powerful kind, when it is stated that plates from 9 in. to 15 in. thick
are formed with a length of 16 ft. and a breadth of 4 ft. The plates are
bent, while red hot, by enormous hydraulic pressure, applied to certain
blocks, upon which the plates are laid, the block having a height adjusted
according to the curve required. The operation requires great care, as it
must be accomplished without straining the parts in a manner injurious to
the strength of the plate.
Fig. 71.—Section of H.M.S. Inconstant.
Fig. 71 on the next page is the section of another ship of war, the Inconstant,
which has not, like the Hercules, been designed to withstand the
impact of heavy projectiles, but has been built mainly with a view to speed.
The Inconstant has only a thin covering of iron plating, except in that
portion of the side which is above water, where there is a certain thickness
of iron diminishing from the water-line upwards, but not enough to entitle
the Inconstant to be classed as an armoured vessel. This ship, however,
may be a truly formidable antagonist, for she carries a considerable number
of heavy guns, which her speed would enable her to use with great effect
against an adversary incapable of manœuvring so rapidly. She could give
153chase, or could run in and deliver her fire, escaping by her speed from
hostile pursuit in cases where the slower movements of a ponderous ironclad
would be much less effective. The Inconstant carries ten 12–ton guns
of 9 in. calibre, and six 6–ton 7 in. guns, all rifled muzzle-loaders, mounted
on improved iron carriages, which give great facilities for handling them
154The ship is a frigate 338 ft. long and 50 ft. broad, with a depth in the hold
of 17 ft. 6 in. She is divided by bulkheads into eleven water-tight compartments.
The engines are of 6,500 indicated horse-power, and the
vessel attains an average speed of more than 18½ miles per hour.
Fig. 72.—Section, Elevation, and Plan of Turret of H.M.S. Captain.
Fig. 73.—H.M.S. Captain.
A new system of mounting very heavy naval guns was proposed by
Captain Coles about 1861. This plan consists in carrying one or two very
heavy guns in a low circular tower or turret, which can be made to revolve
horizontally by proper machinery. The turret itself is heavily armoured,
so as to be proof against all shot, and is carried on the deck of the ship,
which is so arranged that the guns in the turret can be fired at small
angles with the keel. The British Admiralty having approved of Captain
156Coles’ plans, two first-class vessels were ordered to be built on the turret
system. These were the Monarch and the Captain—the latter of which
we select for description on account of the melancholy interest which attaches
to her. On page 155 a diagram is given representing the profile of
the Captain, in which some of the peculiarities of the ship are indicated—the
turrets with the muzzles of two guns projecting from each being easily
recognized. The Captain was 320 ft. long and 53 ft. wide. She was
covered with armour plates down to 5 ft. below the water-line, as represented
by the dark shading in the diagram. The outer plating was 8 in.
thick opposite the turrets, and 7 in. thick in other parts. It was backed
up by 12 in. of teak; there were two inner skins of iron each ¾ in. thick,
then a framework with longitudinal girders 10 in. deep. The deck was
plated in the spaces opposite the turrets with iron 1½ in. thick. The Captain
was fitted with twin screws—that is, instead of having a single screw, one
was placed on each side, their shafts being, of course, parallel with the
vessel’s length. The object of having two screws was not greater power,
for it is probable that a single screw would be more effectual in propelling
the ship; but this arrangement was adopted because it was considered
that, had only one screw been fixed, the ship might easily be disabled by
the breaking of a blade or shaft; whereas in the case of such an accident
to one of the twin screws, the other would still be available. The twin
screws could also be used for steering, and the vessel could be controlled
without the rudder, as the engines were quite independent of each other,
each screw having a separate pair. The diameter of the screws was 17 ft.
The erections which are shown on the deck between the turrets afforded
spacious quarters for the officers and men. These structures were about
half the width of the deck, and tapered off to a point towards the turrets,
so as leave an unimpeded space for training the guns, which could be fired
at so small an angle as 6° with the length of the vessel. Above these
erections, and quite over the turrets, was another deck, 26 ft. wide, called
the “hurricane deck.” The ship was fully rigged and carried a large
spread of canvas. But the special features are the revolving turrets, and
one of these is represented in detail in Fig. 72, which gives a section, part
elevation, and plan. Of the construction of the turret, and of the mode in
which it was made to revolve, these drawings convey an idea sufficiently
clear to obviate the necessity of a minute description. Each turret had an
outside diameter of 27 ft., but inside the diameter was only 22 ft. 6 in., the
walls being, therefore, 2 ft. 3 in. thick—nearly half this thickness consisting
of iron plating. Separate engines were provided for turning the turrets,
and they could also be turned by men working at the handles shown in
the figures. Each turret carried two 25–ton Armstrong guns, capable of
receiving a charge of 70 lbs. of gunpowder, and of throwing a 600 lb. shot.
After some preliminary trials the Captain was sent to sea, and behaved
so well, that Captain Coles and Messrs. Laird, her designer and contractors,
were perfectly satisfied with her qualities as a sea-going ship. She
was then sent in the autumn of 1870 on a cruise with the fleet, and all
went well until a little after midnight between the 6th and 7th September,
1870, when she suddenly foundered at sea off Cape Finisterre. The news
of this disaster created a profound sensation throughout Great Britain, for,
with the exception of nineteen persons, the whole crew of five hundred
persons went down with the ship. Captain Coles, the inventor of the turrets,
was in the ill-fated vessel and perished with the rest, as did also Captain
Burgoyne, the gallant commander, and the many other distinguished naval
157officers who had been appointed to the ship; among the rest was a son of
Mr. Childers, then First Lord of the Admiralty. Although the night on
which this unfortunate ship went down was squally, with rain, and a heavy
sea running, the case was not that of an ordinary shipwreck in which a
vessel is overwhelmed by a raging storm. It might be said, indeed, of the
loss of the Captain as of that of the Royal George:
“It was not in the battle;
No tempest gave the shock;
She sprang no fatal leak;
She ran upon no rock.”
Fig. 74.
Fig. 75.
One of the survivors, Mr. James May, a gunner, related that, shortly after
midnight he was roused from his sleep by a noise, and feeling the ship
uneasy, he dressed, took a light, and went into the after turret, to see if the
guns were all right. He found everything secure in the turret, but that
moment he felt the ship heel steadily over, and a heavy sea having struck
her on the weather side, the water flowed into the turret, and he got out
through the hole in the top of the turret by which the guns were pointed,
only to find himself in the water. He swam to the steam-pinnace, which
he saw floating bottom upwards, and there he was joined by Captain
Burgoyne and a few others. He saw the ship turn bottom up, and sink
stern first, the whole time from her turning over to sinking not being more
than a few minutes. Seeing the launch drifting within a few yards, he
called out, “Jump, men! it is your last chance.” He jumped, and with
three others reached a launch, in which were fifteen persons, all belonging
to the watch on deck, who had found means of getting into this boat. One
of these had got a footing on the hull of the ship as she was turning over,
and he actually walked over the bottom of the vessel, but was washed off
by a wave and rescued by those who in the meantime had got into the
launch. It appears that Captain Burgoyne either remained on the pinnace
or failed to reach the launch. Those who were in that boat, finding the
captain had not reached them, made an effort to turn their boat back to
pick him up, but the boat was nearly swamped by the heavy seas, and they
were obliged to let her drift. One man was at this time washed out of the
boat and lost, after having but the moment before exclaimed, “Now, lads,
I think we are all right.” After twelve hours’ hard rowing, without food or
water, the survivors, numbering sixteen men and petty officers and three
boys, reached Cape Finisterre, where they received help and attention. On
their arrival in England, a court-martial was, according to the rules of the
service, formally held on the survivors, but in reality it was occupied in
investigating the cause of the catastrophe. The reader may probably be
able to understand what the cause was by giving his attention to some
general considerations, which apply to all ships whatever, and by a careful
examination of the diagrams, Figs. 74 and 75, which are copied from diagrams
that were placed in the hands of the members of the court-martial.
The letters b and g and the arrows are, however, added, to serve in illustration
of a part of the explanation. The vessel is represented as heeled
over in smooth water, and the gradations on the semicircle in Fig. 74 will
enable the reader to understand how the heel is measured by angles. If
the ship were upright, the centre line would coincide with the upright line,
marked o on the semicircle, and drawn from its centre. Suppose a level
line drawn through the centre of the semicircle, and let the circumference
between the point where the last line cuts it and the point o be divided
into ninety equal parts, and let these parts be numbered, and straight lines
158drawn from the centre to each point of division. In the figure the lines
are drawn at every fifth division, and the centre line of the ship coincides
with that drawn through the forty-fifth division. In this case the vessel is
said to be inclined, or heeled, at an angle of forty-five degrees, which is
usually written 45°. In a position half-way between this and the upright
the angle of heel would be 22½°, and so on. The reader no doubt perceives
that a ship, like any other body, must be supported, and he is probably
aware that the support is afforded by the upward pressure of the water.
He may also be familiar with the fact that the weight of every body acts
upon it as if the whole weight were concentrated at one certain point, and
that this point is called the centre of gravity of the body. Whatever may
be the position of the body itself, its centre of gravity remains always at
the same point with reference to the body. When the centre of gravity
happens to be within the solid substance of a body, there is no difficulty in
thinking of the force of gravitation acting as a downward pull applied at
the centre of gravity. But this point is by no means always within the
substance of bodies: as often as not it is in the air outside of the body.
Thus the centre of gravity of a uniform ring or hoop is in the centre, where,
of course, it has no material connection with the hoop; but in whatever
position the hoop may be placed, the earth’s attraction pulls it as if this central
point were rigidly connected with the hoop, and a string were attached
to the point and constantly pulled downwards. This explanation of the
meaning of centre of gravity may not be altogether superfluous, for, when
the causes of the loss of the Captain were discussed in the newspapers, it
became evident that such terms as “centre of gravity” convey to the minds
of many but very vague notions. One writer in a newspaper enjoying a
159large circulation seriously attributed the disaster to the circumstance of
the ship having lost her centre of gravity! The upward pressure of water
which supports a ship is the same upward pressure which supported the
water before the ship was there—that is, supported the mass of water which
the ship displaces, and which was in size and shape the exact counterpart
of the immersed part of the ship. Now, this mass of water, considered as
a whole, had itself a centre of gravity through which its weight acted downwards,
and through which it is obvious that an equal upward pressure also
acted. This centre of gravity of the displaced water is usually termed the
“centre of buoyancy,” and, unlike the centre of gravity, it changes its position
with regard to the ship when the latter is inclined, because then the
immersed part becomes of a shape different for each inclination of the ship.
Now, recalling for an instant the fundamental law of floating bodies—namely,
that the weight of the water displaced is equal to the weight of the
floating body—we perceive that in the case of a ship there are two equal
forces acting vertically, viz., the weight of the ship or downward pull of
gravitation acting at G, Fig. 74, the centre of gravity of the ship, and an
equal upward push acting through B, the centre of buoyancy. It is obvious
that the action of these forces concur to turn a ship placed as in Fig. 74
into the upright position. It is by no means necessary for this effect that
the centre of gravity should be below the centre of buoyancy. All that is
requisite for the stability of a ship is, that when the ship is placed out of the
upright position, these forces should act to bring her back, which condition
is secured so long as the centre of buoyancy is nearer to the side towards
which the vessel is inclined than the centre of gravity is. When there is no
other force acting on a ship or other floating body, these two points are
always in the same vertical line. The two equal forces thus applied in
parallel directions constitute what is called in mechanics a “couple,” and
the effect of this in turning the ship back into the upright position is the
same as if a force equal to its weight were applied at the end of a lever
equal in length to the horizontal distance between the lines through B and
160G. The righting force, then, increases in proportion to the horizontal distance
between the two points, and it is measured by multiplying the weight
of the ship in tons by the number of feet between the verticals through G
and B, the product being expressed in statical foot-tons, and representing
the weight in tons which would have to be applied to the end of a lever
1 ft. long, in order to produce the same turning effect. When a ship is kept
steadily heeled over by a side wind, the pressure of the wind and the resistance
of the water through which the vessel moves constitute another
couple exactly balancing the righting couple. The moment of the righting
couple, or the righting force, or statical stability as it is also called, is
determined by calculation and experiment from the design of the ship, and
from her behaviour when a known weight is placed in her at a known distance
from the centre. Such calculations and experiments were made in
the case of the Captain, but do not appear to have been conducted with
sufficient care and completeness to exhibit her deficiency in stability. After
the loss of the ship, however, elaborate computations on these points were
made from the plans and other data. The following table gives some of
the results, with the corresponding particulars concerning the Monarch
for the sake of comparison:
Monarch.
Captain.
I.
Angle at which the edge of the deck is immersed
28°
14°
II.
Statical righting force in foot-tons at the angle at which the deck is immersed
12,542
5,700
III.
Angle of greatest stability
40°
21°
IV.
Greatest righting force in foot-tons
15,615
7,100
V.
Angle at which the righting force ceases
59°
54°
VI.
Reserve of dynamical stability at an angle of 14° in dynamical foot-tons
6,500
410
From No. V. in the above table we learn that if the Captain had been
heeled to 54°, the centre of gravity would have overtaken the centre of
buoyancy—that is, the two would have been in one vertical line. Any
further heeling would have brought the points into the position shown in
Fig. 75, where it is obvious that the action of the forces is now to turn the
vessel still more on its side, and the result is an upsetting couple instead
of a righting couple.
These figures and considerations refer to the case of the vessel floating
in smooth water, but the case of a vessel floating on a wave is not different
in principle. The reader may picture to himself the diagrams inclined so
that the water-line may represent a portion of the wave’s surface; then he
must remember that the very action which heaves up the water in a sloping
surface is so compounded with gravity, that the forces acting through
G and B retain nearly the same position relatively to the surface as before.
No. VI. in the foregoing table requires some explanation. To heel a
ship over to a certain angle a certain amount of work must be done, and
in the scientific sense work is done only when something is moved through
a space against a resistance. When the weight of a ton is raised 1 ft. high,
one foot ton of work is said to be done; if 2 tons were raised 1 ft., or 1 ton
were raised 2 ft., then two foot-tons of work would be done, and so on. The
161same would be the case if a pressure equal to those weights were applied
so as to move a thing in any direction through the same distances. It
should be carefully noticed that the foot-ton is quite a different unit in this
case from what it is as the moment of a couple. If we heel a ship over by
applying a pressure on the masts, it is plain that the pressure must act
through a certain space, and the same heel could be caused either by
means of a smaller pressure or a greater, according as we apply it higher up
or lower down; but the space through which it must act would vary, so
that the product of the pressure and space would, however, be always the
same. No. VI. shows the amount of work that would have to be done in
order completely to upset each of the vessels when already steadily heeled
over to 14°. The amounts in the two cases are so different that we can
easily understand how a squall which would not endanger the Monarch
might throw the Captain over. A squall suddenly springing up would do
more than heel a vessel over to the angle at which it is able to maintain it:
it would swing it beyond that position by reason of the work done on the
sails as they are moving over with the vessel, and the latter would come
to a steady angle of heel only after a series of oscillations. Squalls, again,
which, although suddenly springing up in this manner, could not heel the
ship over beyond the angle where the stability vanishes, might yet do so if
they were intermittent and should happen to coincide in time with the
oscillations of the ship—just as a series of very small impulses, coinciding
with the time of the vibrations of a heavy pendulum, may accumulate so as
to increase the range of vibration to any extent. It is believed that in the
case of the Captain the pressure of the wind on the underside of the hurricane
assisted in upsetting the vessel. This, however, could only have
exerted a very small effect compared to that produced by the sails. The
instability of the Captain does not appear to have been discovered by such
calculations as were made before the vessel went to sea. It was observed,
however, that the ship when afloat was 1 ft. 6 in. deeper in the water than
she should have been—in other words, the freeboard, or side of the ship out
of the water, instead of being 8 ft. high as intended, was only 6 ft. 6 in., and
such a difference would have a great effect on the stability.
Fig. 76.—H.M.S. Glatton.
The turret system has been applied to other ships on quite a different
plan. Of these the Glatton is one of the most remarkable. Her appearance
is very singular, and totally unlike that which we look for in a ship,
as may be seen by an inspection of Fig. 76, page 162. The Glatton, which
was launched in 1871, is of the Monitor class, and was designed by Mr. E.
J. Reed, who has sought to give the ship the most complete protection.
With this view the hull is covered with iron plates below the water-line,
and the deck also is cased with 3 in. iron plates, to resist shot or shell falling
vertically. The base of the turret is shielded by a massive breastwork,
which is a peculiarity of this ship. The large quantity of iron required for
all these extra defences has, of course, the effect of increasing the immersion
of the vessel, and therefore of diminishing her speed. The freeboard
when the ship is in ordinary trim is only 3 ft. high, and means are provided
for admitting water to the lowest compartment, so as to increase the immersion
by 1 ft., thus reducing the freeboard to only 2 ft. when the vessel
is in fighting trim, leaving only that small portion of the hull above water
as a mark for the enemy. The water ballast can be pumped out when no
longer needed. The Glatton is 245 ft. long and 54 ft. broad, and she draws
19 ft. of water with the freeboard of 3 ft., displacing 4,865 tons of water,
while, with the 2 ft. freeboard, the displacement is 5,179 tons. This ship
162cost £210,000. Mr. Reed
wished to construct a vessel
of much larger size on the
same plan—a proposal to
which, however, the Admiralty
did not then consent.
The Glatton is, nevertheless,
one of the most
powerful ships of war ever
built, and may be considered
as an impregnable floating
fortress. Above the water-line
the hull is covered with
armour plates 12 in. thick,
supported by 20 in. of teak
backing, and an inner layer
of iron 1 in. thick. Below
the water-line the iron is 8
in. thick, and the teak 10 in.
The revolving turret carries
two 25–ton guns, firing each
a 600 lb. shot, and is covered
by a massive plating of iron
14 in. in thickness. Besides
this the base of the turret is
protected by a breastwork
rising 6 ft. above the hull.
This breastwork is formed
of plates 12 in. thick, fastened
on 18 in. of teak. The
turret rises 7 ft. above the
breastwork, and therefore
the latter in no way impedes
the working of the guns.
The Glatton has a great
advantage over all the other
turret ships in having a perfectly
unimpeded fore range
for her guns, for there is no
mast or other object to prevent
the guns being fired
directly over the bow. There
are no sails, the mast being
intended only for flying signals
and hoisting up boats,
&c. The hull is divided by
vertical partitions into nine
water-tight compartments,
and also into three horizontal
flats—the lowest being
air-tight, and having arrangements
for the admission
and removal of water,
163as already mentioned.
The stem of the
ship is protruded
forwards below the
water for about 8 ft.,
thus forming a huge
ram which would itself
render the Glatton
a truly formidable
antagonist at
close quarters even
if her guns were not
used. The engines
are capable of being
worked up to 3,000
horse-power, giving
the ship a speed of
9½ knots per hour,
and means are provided
for turning
the turret by steam
power. The turret
can be rotated by
manual labour, requiring
about three
minutes for its complete
revolution, but
by steam power the
operation can be
effected in half a minute.
The commander
communicates
his orders from the
pilot-house on the
hurricane deck to
the engine-room,
steering-house, and
turret, by means of
speaking-tubes and
electric telegraphs.
The Glatton was
not designed to be
ocean-going, but is
intended for coast
defence.
Fig. 77.—H.M.S. Thunderer.
The British navy
contains two powerful
turret-ships
constructed on the
same general plan
as the Glatton, but
larger, and capable
of steaming at a
164greater speed, and of carrying coal for a long voyage. These sister ships
are named the Devastation, Fig. 69, and the Thunderer, Fig. 77. The Thunderer
has two turrets and a freeboard of 4 ft. 6 in. Space is provided for
a store of 1,800 tons of coal, of which the Glatton can carry only 500 tons.
The vessel is fitted with twin screws, turned by two pairs of independent
engines, capable of working up to 5,600 horse-power, and she can steam
at the rate of 12 knots, or nearly 14 miles, an hour. With the large supply
of coal she can carry, the Thunderer could make a voyage of 3,000 miles
without re-coaling. Though the freeboard of the heavily-plated hull is
only 4 ft. 6 in., a lighter iron superstructure, indicated in the figure by the
light shading, rises from the deck to the height of 7 ft., making the real
freeboard nearly 12 ft. This gives the ship much greater stability, and
prevents her from rolling heavily when at sea. The length is 285 ft. and
the width 58 ft., and the draught 26 ft. The hull is double, the distance
between the outer and inner skins of the bottom being 4 ft. 6 in. The
framing is very strong and on the longitudinal principle, and the keel is
formed of Bessemer steel. Each turret is 24 ft. 3 in. in internal diameter,
and is built with five layers of teak and iron. Beginning at the inside,
there is a lining of 2⅝ in. iron plates; then 6 in. of teak in iron frames,
arranged horizontally; 6 in. of armour plates; 9 in. of teak, placed vertically;
outside of all, 8 in. armour plates. Each turret carries two Fraser
35–ton guns, rifled muzzle-loaders. The turrets revolve by hand or by
steam-power. There are no sails, and thus a clear range for the guns
is afforded fore and aft. The bases of the turrets are protected by the
armoured breastwork, of which a portion is seen in the figure in advance
of the fore turret.
Another very powerful ship of war, which possesses some special
features, is represented in the diagram on page 165, Fig. 78. This vessel,
named the König Wilhelm, was built at Blackwall for the Prussian Government
by the Thames Ironworks and Steam Shipbuilding Company, from
designs by Mr. Reed. Her length is 365 ft., width 60 ft.; burthen, 6,000
tons; displacement, 8,500 tons. She is framed longitudinally, that is,
girders pass from end to end, about 7 ft. apart, and the stem projects into
a pointed ram. In this case also the hull is double; there is, in fact, one
hull within another, with a space of 4½ ft. between them. The armour
plates are 8 in. in thickness, with 10 in. of teak backing; but on the less
important parts the thickness of the iron is reduced to 6 in., and in some
places to 4 in. This ship has a broadside battery, and there are no turrets,
but on the deck there are, fore and aft, two semicircular shields, formed of
iron plates and teak, pierced with port-holes for cannon, and also with
loop-holes for muskets. From these a fore-and-aft fire may be kept up.
The ship is fully rigged, and has also steam engines of 7,000 horse-power,
by Maudslay and Co. Her armament consists of four three-hundred-pounders,
capable of delivering fore-and-aft as well as broadside fire, and
twenty-three other guns of the same size between decks. These guns are
all Krupp’s steel breech-loaders.
The great contest of armour plates versus guns has already been alluded
to, and to the remarks then made it may be added that, while on the one
hand, guns weighing 110 tons are mounted in turrets, ships are already
designed with 18 in. and even 20 in. of steel armour plates. It would be
very difficult to predict which side will sooner reach the limit beyond which
increase of size and power cannot go. The gradual increase of thickness
of plating, attended by increased weight of guns, projectiles, and charges
166of powder, may be illustrated by stating in a condensed form a few
details of some ships, as regards the thickness of armour, and its resisting
power, which is nearly in proportion to the square of its thickness; and
also some particulars respecting the guns originally carried by those ships.
Warrior.
Hercules.
Glatton.
Thunderer.
Victoria.
Date when completed
1861
1868
1872
1877
1889
Thickness of iron plating in inches
4½
9
12
14
18
Relative resisting power of plating
20
81
144
196
324
Guns carried
Cast iron, smooth bore
Wrought iron, rifled
Wrought iron, rifled
Wrought iron, rifled
Steel, Rifled
Weight of guns in tons
4¾
18
25
35
111
Charge of powder in lbs.
16
60
70
120
960
Weight of projectiles in lbs.
68
400
600
700
1,800
Destructive power of projectiles in foot-tons
452
3,863
5,165
8,404
56,000
167One of the latest additions out of the thirty or forty armoured ships that
have been added to the British Navy since the preceding pages were
written is included in the above table for the sake of comparison. Our
ironclad fleet now includes vessels protected and armed in many
different ways. Some have the protective armour extended continuously
along the water-line, others have it for only a greater or less part of their
length. The armaments are also very diverse as to the size of the guns
and the way in which they are mounted. A few carry one or two of the
huge 110–ton gun mounted in massive revolving turrets; others have
their guns in central batteries, or in barbettes, and others again are arranged
as broadside ships; while these plans are also variously combined so as to
form a great number of different types. In the ships built within the last 15
years, steel has been almost invariably used instead of iron for the armour-plating.
A great increase of speed has been obtained in late years. The
largest British armoured ships yet launched have displacements between
10,000 and 12,000 tons, but another class of first-rate line-of-battle ships
of still greater size is in process of construction, and of these it is estimated
that four will be completed in 1893. They are all of the same
design and armament, and will have a displacement of 14,150 tons, a
length of 380 feet, and a breadth of 75 feet. The armour plates at the
sides will be 18 inches thick. Each ship will carry four 67–ton breech
loading rifled guns, ten 6–inch quick firing guns, and 18 other
smaller guns, also quick firing. These vessels are expected to realize a
speed of about 20 miles per hour; but this is somewhat less than a few
of the heavy ironclads now afloat have given by actual trial, a rate
equal to 21⅓ miles an hour having been attained by some. Several of our
rapid unarmoured cruisers are able to steam at 25 miles an hour.
Before the close of 1894, the British navy possessed no fewer than eight
of the largest armoured line of battle-ships mentioned in the foregoing
paragraph, each being of 14,150 tons displacement, and having engines of
13,000 horse-power. At the same period there were in course of construction
four ships surpassing even these in tonnage, though of somewhat
less engine-power. Two were building at Portsmouth, to be called the
Majestic and the Royal George, whilst the Jupiter was in progress at
Glasgow and the Mars at Birkenhead. All these are very heavily
armoured vessels, each displacing 14,900 tons, provided with engines of
12,000 horse-power, and a very effective armament of guns. Among the
powerful ships of the navy may now also be noted the Blake, the Blenheim,
which, although the displacement is only 500 tons greater than that of
König Wilhelm, have engines of nearly three times the power, namely,
of 20,000 horse-power. Of large armoured ships, namely, those of 9,000
tons and upwards, Great Britain now has afloat at least fifty; and the
advance that has taken place in the size and power of war-ships during
the last twenty years may be inferred by reference to the foregoing
paragraphs giving the dimensions, &c., of the Glatton and the Thunderer,
which paragraphs are, for the sake of comparison, allowed to appear as
they did in the first edition (1876) of this book. Besides these very large
armoured vessels, of which the smallest is nearly twice as big as the
largest of twenty-five years ago, the British navy comprises ships of every
size and for every purpose, and so many of them that their names and
classifications would occupy many pages.
Two recent additions representing new type of ships claim notice
before this article is concluded. These are first the Terrible, with a
168sister ship the Powerful. The former, of which a representation[3] is given
in Plate V., is pronounced, for its size, armour, armament, and speed
taken together, to be the most powerful cruiser in the world. The length
is 538 ft., breadth 71 ft., depth 43 ft., and the displacement is 14,250 tons.
A special object in the design of this vessel was high speed, and she is
provided with twin-screws and two engines, the combined effort of which
is equal to 25,000 horse-power. There are forty-eight boilers and four funnels,
the ship being capable of carrying 3,000 tons of coal. The vessel is
built on the lines of the great Atlantic steamers, and the engines, guns, and
magazines are protected by a thick curved armour deck. The vessel has
a speed of 22 knots, or 25⅓ miles per hour. Her armament consists of
two 22–ton guns, twelve 6–in. quick-firing, and many other smaller
machine guns, and she carries besides four submerged torpedo tubes.
A second ship to be noted is amongst those designed mainly to exceed all
other craft in speed, and ranging in tonnage from 3,800 to 4,500. The
Janus, a torpedo-boat destroyer of this class, was found, at a recent
trial over a measured mile, to attain the then unexampled speed of 28
knots, or 32¼ miles per hour. But even this has been beaten by a new
torpedo-boat destroyer, built by Messrs. Yarrow at Poplar for the Russian
Government, and launched in August, 1895. This vessel, within a few
hours after leaving the stocks, cut through the water at the rate of 30·285
knots, or nearly 35 miles, per hour.
A sad fate befell the Victoria, which was one of the heaviest armed of
British ships (vide page 129), when taking part in some naval manœuvres
off Tripoli, on the Syrian coast, where she was the flag-ship of Admiral
Tryon, commander-in-chief of the squadron. On the 22nd June, 1893,
in consequence of an inconsiderate order given by the admiral himself,
the Victoria was struck by the formidable ram of the Camperdown
(10,600), and in fifteen minutes turned over and sank in sight of the
whole fleet, carrying down with her the admiral, 30 officers, and 320
men, out of a crew of 600. [1895.]
Fig. 78b.—Firing at a floating battery.
PLATE XI. H.M.S. “TERRIBLE.”
169
Fig. 79.—Krupp’s Works, at Essen, Prussia.
FIRE-ARMS. — THE MILITARY RIFLE. — RIFLED CANNON. — The Fraser-Woolwich Guns, 1867–1880. — MACHINE GUNS.
The invention of gunpowder—or rather its use in war—appears at first
sight a device little calculated to promote the general progress of
mankind. But it has been pointed out by some historians that the introduction
of gunpowder into Europe brought about the downfall of the feudal
system with its attendant evils. In those days every man was practically a
soldier: the bow or the sword he inherited from his father made him ready
for the fray. But when cannons, muskets, and mines began to be used, the
art of war became more difficult. The simple possession of arms did not
render men soldiers, but a long special training was required. The greater
cost of the new arms also contributed to change the arrangements of
society. Standing armies were established, and war became the calling of
only a small part of the inhabitants of a country, while the majority were
left free to devote themselves to civil employments. Then the useful arts
of life received more attention, inventions were multiplied, commerce began
to be considered as honourable an avocation as war, letters were cultivated,
and other foundations laid for modern science. If such have really been
the indirect results of the invention of gunpowder, we shall hardly share the
regret of the fine gentleman in “Henry IV.”:
“That it was great pity, so it was,
That villanous saltpetre should be digged
Out of the bowels of the harmless earth,
Which many a good tall fellow had destroyed
So cowardly.”
We often hear people regretting that so much attention and ingenuity as
are shown by the weapons of the present day should have been expended
170upon implements of destruction. It would not perhaps be difficult to show
that if we must have wars, the more effective the implements of destruction,
the shorter and more decisive will be the struggles, and the less the total
loss of life, though occurring in a shorter time. Then, again, the exasperated
and savage feelings evoked by the hand-to-hand fighting under the
old system have less opportunity for their exercise in modern warfare,
which more resembles a game of skill. But the wise and the good have in
all ages looked forward to a time when sword and spear shall be everywhere
finally superseded by the ploughshare and the reaping-hook, and the
whole human race shall dwell together in amity. Until that happy time
arrives—
“Till the war-drum throbs no longer, and the battle flags are furl’d
In the Parliament of man, the Federation of the world—
When the common sense of most shall hold a fretful realm in awe,
And the kindly earth shall slumber, lapt in universal law,”—
we may consider that the more costly and ingenious and complicated the
implements of war become, the more certain will be the extension and the
permanence of civilization. The great cost of such appliances as those we
are about to describe, the ingenuity needed for their contrivance, the elaborate
machinery required for their production, and the skill implied in their
use, are such that these weapons can never be the arms of other than
wealthy and intelligent nations. We know that in ancient times opulent
and civilized communities could hardly defend themselves against poor
and barbarous races. But the world cannot again witness such a spectacle
as Rome presented when the savage hordes of Alaric swarmed through her
gates, and the mighty civilization of centuries fell under the assaults of the
northern barbarians. In our day it is the poor and barbarous tribes who
are everywhere at the mercy of the wealthy and cultivated nations. The
present age has been so remarkably fertile in warlike inventions, that it
may truthfully be said that the progress made in fire-arms and war-ships
within the second half of the nineteenth century surpasses everything
that had been previously accomplished from the time gunpowder came
into use. Englishmen have good reason to be proud of the position taken
by their country, and may feel assured that her armaments will enable
her to hold her own among the most advanced nations of the world.
The subject of fire-arms embraces a very wide ground, as will appear
if we consider the many different forms in which these weapons are constructed
in order best to serve particular purposes. Pertaining to this
subject, attention must also be directed to the modern projectiles and to
the newer explosives that have largely taken the place of ordinary gunpowder.
The shot gun, fowling-piece, and sporting rifle properly come
under the head of fire-arms, and in the march of improvement these
forms have most commonly been in advance of military muskets and
rifles, the ingenuity bestowed on all their details being worthy of admiration.
Nevertheless it is to the implements of war that general interest
attaches; for on them depends so much the fate of battles and the
destiny of nations, that whenever any country is engaged in war the
question of arms becomes one of surpassing importance, enlisting the
patriotic instincts of every citizen. Hence in the following pages our
space will be devoted mainly to weapons of war, and more particularly to
those that have been adopted by our own country.
Everyone of course is aware that guns, cannon, and gunpowder are by
no means inventions of the nineteenth century; but there are fewer
171acquainted with the fact that rifling, breech-loading, machine guns, and
revolvers were all invented and tried hundreds of years before. The
devices by which some of these ideas were sought to be realised in past
ages appear to us in some instances very primitive, not to say childish,
when compared with modern work: but it must be remembered that
nearly all the appliances required for producing such weapons had
themselves to wait for their invention until the nineteenth century; such,
for instance, as the steam-hammer, powerful and accurate tools, refined
measuring implements, material entirely reliable such as the new steel,
and also scientific investigations of all the conditions involved. The
military fire-arms are of so many different forms and patterns that we
can deal here with but a selection from the various services. If a
rough classification had to be made, the most obvious distinction would
be between the weapons the soldier carries in his hands (small-arms) and
those which are mounted on some kind of carriage and discharge projectiles
of much greater weight (ordnance). Ordnance again includes
guns mounted on forts, carried in ships, or taken with an army into the
field, in each case coming into action under different conditions. Partaking
somewhat of the nature of both field-guns and of small-arms are the
machine guns, of which the French mitrailleur was the first example,
afterwards developing into much more effective weapons in the hands of
Gatling, Gardner, Nordenfelt, Maxim, and Hotchkiss.
As much will have to be said about rifling the bores of muskets and
cannon, we may here explain the nature and object of this device. The
projectiles used in all guns down to comparatively recent times were
almost invariably of spherical form, and could indeed scarcely be otherwise
with smooth-bore weapons. As the diameter of the shot would necessarily
be something less than that of the bore of the barrel, a considerable loss
of power would result from the escape of the powder gases between the
shot and the barrel, which escape is known as windage. Another disadvantage
of the spherical projectile is that for the same weight of metal
the air offers a greater resistance to its passage, and consequently checks
its speed more quickly than that of any other circular form; for the air
resistance is proportional to the square of the diameter, and therefore if
we take a ball of 1 in. diameter and a cylinder of 1 in. in length, each having
the same weight of metal, the diameter of the cylindrical shot will be a
little more than four-fifths of an inch, and the air resistance to the ball
will be exactly half as much again as to the cylinder, that is, in the proportion
of 3 to 2. Again, the passage of the spherical shot within the
barrel of the gun will not be in a straight line, but in a series of rebounds
from side to side, and its direction on leaving the muzzle will depend upon
which part of the bore it just before impinges on, as from that it will also
take a rotatory “twist” that will in part determine its path through the
air.
Now if an elongated projectile were fired from a smooth-bore gun, its
course through the air would be erratic to a degree impossible to the
spherical shot, for it would turn end over end with deviations that would
make aiming impracticable. But if the elongated projectile is made to
spin rapidly enough about its longitudinal axis, it flies through the air
quite steadily, the axis of rotation remaining parallel to that of the gun
throughout the whole flight. The steadiness due to rapid rotation has
familiar examples in spinning tops, in gyroscopic tops, in the way arrows
are feathered so that the air may cause them to revolve axially, and so
172on. The axial rotation of the projectile is effected by ploughing out in
the cylindrical barrel of the gun a number of spiral or twisting grooves,
which the projectile is compelled to follow as it travels along the barrel,
either by means of corresponding protuberances formed upon its surface
in the first instance, as in Jacob’s bullets, or by studs let into it, as in the
studded shots and shells for ordnance which constituted at one time the
regulation plan adopted by the British Government; or otherwise by
making the force of the explosion expand some portion of the projectile
in such a manner that this portion shall completely fill up the grooves,
thus preventing windage, and causing the projectile to follow the twist
of the grooves. This is the more general method, especially since the
adoption of breech-loading. The Lancaster rifling, and that advocated
by Whitworth, are the same in principle, but differ in appearance, from
the section of the barrel being made in the one case oval, in the other
hexagonal or polygonal, but with the twist necessary to produce rotation.
Incident to the discharge of all fire-arms, great and small, is a phenomenon
of which we have to speak, because it is one which in the mounting
of heavy ordnance especially has to be taken into account. And as it
also illustrates in a very direct way one of the most general laws of nature,
while people often have very vague and erroneous ideas of its cause and
operation, it deserves the reader’s attention. In gunnery it is called the
recoil, and is familiar to anyone who has ever fired a pistol, fowling-piece,
or rifle, in the kick backwards felt at the moment of the discharge. This
law is in operation whenever the condition of a body in respect to its rest
or motion is changing. That is, whenever a body at rest has motion
given to, or if when already moving it is made to go faster or slower, or to
stop, or when the direction of the motion is changed from that in a straight
line. Now although these changes or actions are frequently occurring
before our eyes, the operation in them of Newton’s third law of motion
does not generally present itself to common observation. This third law
was stated by Sir Isaac Newton thus:—“To every action there is always
an opposite and equal reaction.” Now the expanding gases due to the
gunpowder explosion press the bullet forwards and the barrel (with its
attachments) backwards, with the same pressure in both cases, but at the
end of the bullet’s passage along the bore the same velocity is not imparted
to the two bodies, because the same pressure acting for the same time on
bodies of unequal mass always produces velocities that are inversely
proportional to the masses. The reader should try to acquire this conception
of mass, remarking that it is a something quite distinct from that
of weight. A given lump of metal, for instance, would have exactly the
same mass in any part of the universe, whereas its weight would depend
upon its position; as, for instance, at the distance from the earth of
the moon’s orbit, it would weigh only as 1 3600th part of its weight at the
earth’s surface, and if it could be carried to the very centre of the earth
it would there have no weight at all. Though the lump of metal will have
different weights at different parts of the earth’s surface, it has been found
(by experiment) that the weights of bodies at any one place are proportional
to their masses. Therefore the same numbers that express the
weights of bodies might also express their masses; but for certain
good reasons these quantities are referred to different units. In
England a piece of metal weighing 32 lbs. under standard conditions is
said to have mass = 1; and so on. As with the same pressure acting for
the same time, the velocities imparted are inversely proportional to the
173masses, it follows that the number expressing the velocity multiplied by
that representing the mass in each such case of action and reaction will
give the same product, or in other words the amount of motion (momentum)
will be the same. This is what Newton meant by saying the reaction
is equal to the action. We may now by way of illustration calculate the
velocity of recoil of a rifle under conditions similar to those that might
occur in practice. Let us suppose that the rifle, including the stock and
all attachments, weighs 10 lbs., and that from it is fired a bullet weighing
one-sixteenth of a pound, with a velocity at the muzzle of 1,200 ft. per
second. To obtain the amount of motion or the momentum, we should
here multiply the number expressing the mass of the bullet by 1,200, but
for our present purpose the weight numbers may be used for the sake of
simplicity; therefore 1 16 x 1,200 = 75 will represent (proportionately) the
forward momentum of the bullet, and according to Newton’s law the
backward momentum of the rifle will be, on the same scale, 75 also. We
must therefore find the number which multiplied by 10 will give 75, and
this obviously is 7·5. That is as much as to say that at the instant the
bullet is leaving the muzzle, the rifle itself, if free to move, would be
moving backward at the speed of 7½ ft. per second. Observe that this
result would be the same if the rifle were fired where weight is non-existent;
nor is the recoil due, as sometimes is erroneously supposed, to the
resistance of the air to the passage of the bullet along the barrel, for even
if the air were abolished, the recoil, so far as due to the masses and
velocities, would remain the same, as indeed may be seen from the fact
of our calculation taking no account of the bore of the rifle or of the
shape of the bullet, circumstances of the utmost importance where atmospheric
resistance is concerned.
The foregoing calculation however involves an assumption not in
exact conformity with actual conditions, by taking for granted that the
centre of gravity of the rifle is in the line of the axis of the barrel, while
in fact this centre is almost always lower, and therefore the kick of the
recoil acts in part as a turning-over push, tending to tilt up the muzzle of
the gun, and for that reason the firer must hold the weapon very firmly
or he will miss his aim. When such a rifle as we have supposed is fired,
say from the shoulder, it would follow from the above calculation that the
backward kick of the recoil is equivalent to a blow from a 10–lb. weight
moving at the speed of 7½ ft. per second. This would certainly be a very
uncomfortable experience, but the backward momentum must be met
somehow. We have supposed that the gun is free to move, but we know
the firer presses it firmly against the muscles of his shoulder, and the
stock of the gun is spread out and provided with a smooth hollow heel
plate, so that any pressure from it is felt as little as possible, especially
as the muscle against which it is applied acts as an elastic pad. With
the rifle thus firmly held we may regard the marksman and his rifle as
forming only one mass, and the centre of gravity of this being now much
below the axis of the barrel, the effect of the recoil tends to overthrow the
man backwards; but he learns to resist this by standing firmly, so that
the elasticity of his whole frame comes into play; and besides this, the
mass factor of the momentum being now so large, the velocity factor
becomes comparatively insignificant.
Although the momenta of gun and projectile are, according to Newton’s
law, equal and opposite, the case is very different with regard to their
energies, or powers of doing work, for the measure of these is jointly mass
174and the square of the velocity. The energy (vis viva) of a body of weight
in pounds = W, moving with the velocity of v feet per second is always
Wv2 64·4, that is, it will do this number of foot-lbs. units of work before it
comes to rest. It would require too much space to demonstrate and fully
explain here what this means, but the reader may refer to our index
under the entries “Energy” and “Work,” or to any modern elementary
treatise on dynamics. If the calculation be made of the energies of the
ball and of the rifle due to our calculated velocities of recoil, it will be
found that that of the ball is 160 times greater than that of the other, and
the ball possesses this energy in a much smaller compass.
Fig. 80.—Trajectory of a Projectile.
The course or track of a
projectile through the air after
it leaves the gun is called the
trajectory, and this has been
studied both experimentally
and theoretically, with interesting
results. Assuming that
the shot passed through empty
space, or that the air offered
no resistance to its passage, it
would be very easy to trace
the path of a projectile. Let
us suppose that Fig. 80 represents
a gun elevated at a high
angle. The moment the projectile
leaves the muzzle, gravity
begins to act upon it, causing
it to move vertically downwards
with ever-increasing velocity
until it finally reaches the
ground; the onward uniform
movement parallel to the axis of the piece being continued all the
time. We could find the position of the projectile at the end of
successive equal periods of time by drawing a straight line AC, a
prolongation of the axis of the piece, or a line of the same inclination;
on this we mark off equal distances representing by scale the
velocity of the projectile per second, the points B, C, D, E being the
positions the projectile would be in at the end of each successive
second if gravity did not act. In order to bring the diagram within
moderate compass, we suppose the projectile to have only the small
velocity of 115 ft. per second. At the end of the first second it would be
at B, but now suppose that gravity is allowed to act for one second, it
would at the end of that time have fallen 16 ft. vertically below B and
have arrived at b. Similarly we may set off by scale on verticals through
C, D, and E distances representing 64 ft., 144 ft., and 256 ft. respectively.
Because, for instance, the ball, without gravity acting, would at the end
of 3 seconds be at D, where we may suppose its course arrested and
gravity then allowed to act for 3 seconds to pull the ball down from its
position of rest at D; at the end of this period, gravity alone acting, its
position would be 144 ft. vertically below D, because gravity pulls a body
that distance in 3 seconds, and the actual position 3 seconds after the
ball had left the muzzle would be at d, after it had described the curved
175path A, b, c, d. Supposing d to be the highest point of the trajectory,
another 3 seconds would bring the ball along a downward curve, and at
the end of 6 seconds from the discharge it would be at a point on the
same level as A. Now the complete curve would be symmetrical on each
side of a vertical line through its highest point, and it would be in fact a
regular parabola with its vertex at d.
The foregoing presupposes that the air offers no resistance to the
passage of the projectile through it. The fact however is quite otherwise,
for no sooner does the projectile begin its flight than its velocity is constantly
diminished by the air’s resistance. Now this resistance is complex,
depending upon a number of different conditions, the effect of which can
be taken into account only by extremely complex calculations. Obviously
it will vary according to the area of the section presented by the projectile
to the line of its flight, and again by the shape of its front, for a pointed
shot will cleave the air with less resistance than one with a flat front.
Then the density of the air at the time will also enter into the calculation.
The mass of the projectile and also its velocity, upon which depend its vis
viva, energy, or power of overcoming resistance in doing work, will also
have to be considered. Most complex of all is the law, or rather laws (i.e.
relations), which connect the air resistance with the velocity; for this relation
no definite expression has been found. It is a function of the velocity
(known only by experiment under defined conditions), and varying with the
velocity itself. Thus for velocities up to 790 ft. per second, it is a function
(determined experimentally) of the second power or square of the velocity;
between 790 ft. per second and 990 ft. per second the law of resistance is
changed and becomes a function of the third power of the velocity;
between 990 ft. and 1,120 ft. velocity the law again changes and is related
to the sixth power of the velocity; between 1,120 ft. and 1,330 ft. the
resistance is again related to the third power of the velocity; and with
higher speeds than that last named it is again more nearly related to the
square of the velocity. It will be seen that to calculate the path of a
projectile is really a very difficult mathematical problem, and indeed one
which can be solved only approximately when all the known data are
supplied.
The air resistance to the motion of a projectile is much greater than
before trial would be supposed. Let us take an experiment that has
actually been recorded, in which a bullet three-quarters of an inch in
diameter, weighing one-twelfth of a pound, was found to have a velocity
of 1,670 ft. per second at a distance of 25 ft. from the gun, and this 50 ft.
farther was reduced to 1,550 ft. per second. Now if the reader will calculate,
according to the formula we have given above, the energy due to the
bullet’s velocity at these points, he will find it must have done 500 foot-lbs.
units of work in traversing the 50 ft., and as this could have been expended
only in overcoming the resistance of the air, we learn that this last must
have been equivalent to a mean or average pressure of 10 lbs. thrusting
the bullet backwards.
It will be interesting to compare the difference in the trajectory of a
projectile under defined conditions, worked out with the air resistance
taken into account, compared with the trajectory when the air is supposed
to be non-existent. We find an example of the former problem fully
worked out by many elaborate mathematical formulæ in Messrs. Lloyd and
Hadcock’s treatise on Artillery. The problem is thus stated:—“An 11–in.
breech-loading howitzer” (a howitzer is a piece of ordnance used for firing
176at high angles) “fires a 600–lb. projectile with an initial velocity of 1,120
foot-sec. at an elevation of 20°. Find the range, time of flight, and angle
of descent.” We shall calculate these points on the suppositions adopted
with regard to Fig. 80, and with no higher mathematics than common
multiplication and division.
It will have been observed that we supposed two motions that really
take place simultaneously to take place successively and independently:
one in the direction of the line of fire, due to the initial velocity; the
other vertically downwards, due to the action of gravity, the final result
being the same. This affords an excellent illustration of another of
Newton’s laws of motion, and should be considered by the reader in this
connection. The law itself admits of being stated in various ways, as
thus:—“Whenever a force acts on a body, it produces upon it exactly the
same change of motion in its own direction, whether the body be originally
at rest or in motion in any direction with any velocity whatever—whether
it be at the same time acted on by other forces or not.” Or again:
“When two forces act in any direction whatever on a body free to move,
they impress upon it a motion which is the superposition (or compounding)
of those that it would receive if each force acted separately.” The
law is given also in the following form (Thomson and Tait):—“When
any forces act on a body, then, whether the body be originally at rest or
moving with any velocity and in any direction, each force produces in the
body the exact change of motion which it would have had had it acted
singly on the body originally at rest.” In all of these expressions the word
“forces” is used, and a very convenient word it is, but it may be noted
in passing, nothing but a word; for it stands for no real self-existing
things, since, apart from observed changes of motion in bodies, forces
for us have no existence. Nevertheless, it is useful for the sake of
abbreviating statements about changes of motion, to regard these actions
as produced by imaginary agents—imagined for the time and for this
purpose, and therefore vainly to be sought for in the realm of reality.
Fig. 81.—Diagram.
In dealing with the trajectory of the howitzer’s
projectile through airless space we have no concern
with its diameter nor with its weight. We
use the little diagram, Fig. 81, to represent the
motions,—c being a horizontal line, a, a vertical
one, the angle at B is therefore a right angle,
and we assume that at A to be 20°. Now, the
most elementary geometry teaches us that every
triangle having these angles will have the lengths
of its sides in the same invariable proportions one to another whatever
may be the size of the triangle itself, and it has been found convenient
to calculate these proportions once for all, not merely for angle 20°, but
for every angle up to 90°. Besides this, distinct names have been given
to the proportions of every side of the triangle to each of the other two
sides. Thus in the triangle before us, if we take a, b, and c to represent
the numbers expressing the lengths of the sides against which they are
placed, a divided by b, that is a ÷ b, or a/b, is called the sine of angle 20°,
while c/b is named the cosine of that angle, etc. These therefore are
numbers which are given in mathematical tables, and we find by these
that sine 20° = 0·3420201, and cosine 20° = 0·9396926, and these with the
177initial velocity give us all the data we require. We may first find the
time the projectile would take to reach the ground level, or strictly that
of the muzzle of the gun at B. Taking t to stand for this time, we know
that AC = 1,120 × t, but CB will be the distance that a body would fall from
rest at C by the influence of gravity in that same time, t, and it is known
by experiment that this distance is 16·1 feet multiplied by the square of
the time from rest in seconds. We have now therefore the length of
the line CB, and put a b = CB AC = 16·1 × t2 1,120 × t = sine 20° = ·3420201, and dividing
numerator and denominator by t and multiplying the above 3rd and 5th
expressions by 1,120, we have
16·1 ×
t =
1,120 × ·3420201
1,120 × ·3420201
and therefore
t =
= 23·7927 secs.
16·1
Having obtained the time, it will be easy to work out the lengths b and a
as 26,648 ft. and 9114·1 ft. respectively; and as c/b = cosine 20°, we have
c = 26,648 × ·9396926 = 25040·8 ft., which is the range. The trajectory will
be a curve (parabola) symmetrical on each side of a vertical line half-way
between A and B, and the length of this line within the triangle will be
equal to half of a, and in half of 23·7927 seconds the projectile, supposed
to move only along the line AC, would reach the point where this vertical
axis intersects AC. If during this half-time it had been falling from rest
at the same intersection, it would have reached a point below by a space
just one quarter of CB (the spaces fallen through being as the squares of
the times), and therefore at this its highest point its distance above AB
would also be one quarter the length of a = 2278·525 ft., which distance
is called the height of the trajectory; and the descending curve being in
every respect symmetrical to the ascending branch, the angle at which
this would be inclined to AB would be 20°, but in the opposite direction to
BAC, while the velocity would be the same as at A. We may now compare
these results with those calculated when the air resistance is taken into
account:—
Without air
With air
resistance.
resistance.
Difference.
Time of descent
23·7927 secs.
22·61 sec.
–1·18 sec.
Angle of descent
20°
23° 49´
+3° 49´
Velocity of descent
1120 foot-secs.
868·8 foot-secs.
–251·2 f.-s.
Range
25040·8 ft.
20,622 ft.
–4418·8 ft.
Height of trajectory
2278·5 ft.
1989 ft.
–288·5 ft.
With the air resistance the trajectory will no longer be a symmetrical
curve: its highest point, instead of being on the vertical line midway
between A and B, will be on one 1,050 ft. nearer to B than to A, and the
descending branch will be steeper than the ascending. The total time,
it will be observed, is less, although the final, and therefore the mean,
velocity, is also less; but this shortening of the time is due to the trajectory
itself being much less in length. The range of the projectile is decreased
178by 4,418 ft., or 1,473 yards, or more than four-fifths of a mile. The loss of
velocity at the descent is very notable, and the reader will find it interesting
to calculate the corresponding loss of energy by the formula already
given.
The reader should now easily understand that the projectile from a
rifle or gun discharged horizontally through airless space at the height
of 16·1 ft. above a level plain would strike the ground in one second at a
range or distance from the gun exactly equal to the initial velocity, or if
the gun were on a tower and its axis 64·4 ft. above the plain, the range
would then be 2V. It will be seen therefore that, corresponding to the
range intended, there must be in general a certain inclination given to the
axis of the piece in aiming, and this is done by means of the sights, one
of which near the muzzle is usually fixed, while that next the breech is
adjustable by sliding along an upright bar, which is graduated so that the
proper elevation may be given for any required range. These graduations
are made from experiments, and of course have reference only to some
standard quantity and quality of ammunition and a standard of weight,
shape, and material in the projectile. Sometimes large pieces of ordnance
are laid by elevation in degrees, etc., marked on their mounting, the
angles being taken from a table prepared for that particular gun and
ammunition, from experiments at different ranges.
After these generalities about fire-arms we may enter upon certain
particulars about the construction of some varieties, beginning with
Fig. 82.—Muzzle-loading Musket and Rifles (obsolete patterns).
A. Brown Bess and Bayonet; B. Brunswick Rifle; C. Enfield Rifle and Bayonet.
In Fig. 82 are represented the muzzle-loading musket and muzzle-loading
rifles which formed the regulation weapons of the British
infantry from the beginning of the century up to the year 1864. Somewhat
slow in its earlier stages was the development of the modern
military rifle from the old smooth bore musket with its flint-lock, which
was the ordinary weapon of the British and other armies up to nearly
the middle of this century. Partly, perhaps, owing to the inherent conservatism
of government departments, and partly to the very serious outlay
involved in arming all the troops of a nation with a new weapon, it has
happened that many improvements in small arms were in use as applied
to sporting guns, long before they were adopted in the regulation weapons
of armies. The advance towards the modern arm of precision has been
made along all the several directions that converge in the latest product,
and it may be said that the most obvious of these are spiral rifling, breech-loading,
and improved ammunition. The improvements in any one of
these particulars would have been of little advantage unless the others
had been kept in line with it. How long antiquated systems may continue
in use may be illustrated by the case of the flint-lock, which was retained
in the British army from the time it superseded the old match-lock,
in the latter part of the seventeenth century, down to almost the middle
of this present nineteenth. It is quite possible that not a few readers
still in their fifties may never have seen a flint-lock outside of a museum,
yet this was the firing apparatus of the weapon that used to be affectionately
known to our soldiers as “Brown Bess,” and that for a century and
a half continued the regulation arm of British troops helping Wellington
180to win his victories, and superseded by the percussion musket only in
1842. The “Brown Bess” of the earlier part of the century had a smooth-bore
barrel of three-quarters of an inch diameter (0·753 inch), and 39 inches
long; this musket weighed, with its bayonet, 11 lbs., 2 oz. The bullet
was spherical, and made of lead, in weight a little over one ounce. The
diameter of the bullet was slightly smaller than the bore of the barrel,
because a closely fitting ball could not be used, on account of the great
force required to push it home with a ram-rod. The bullet was therefore
wrapped in loosely fitting material, called a “patch,” and this made the
gun easy to load, even when the barrel was “fouled” by the solid residues
that always remain after the explosion of gunpowder. “Brown Bess”
was credited with a range of 200 yards, but its want of accuracy was such
that the soldier was directed not to fire until he could see the whites of
the enemies’ eyes. But in 1800 one or two British regiments were armed
with the muzzle-loading rifle known as Baker’s, and again in 1835 these
were provided with the Brunswick rifle. These regiments afterwards became
known as the Rifle Brigade. The bullets in both cases were
spherical, and as the earlier pattern had a seven-grooved barrel, there
was so much difficulty in introducing the bullets into the muzzles that
mallets had to be used. The bullet of the Brunswick rifle was encircled
by a projecting band, which fitted into two rather deep grooves diametrically
opposite to each other in the barrel. This bullet, wrapped in some
slightly greased material, could be readily dropped into the muzzle, and
rammed home without difficulty. Moreover, whereas in Baker’s rifle the
grooves made only a quarter of a turn in the length of the barrel, the
grooves of the Brunswick rifle made more than one complete turn. This
was so much an improvement on “Brown Bess” that the effective range
was more than doubled. For the rank and file of the infantry regiments
the flint-lock smooth-bore musket was, however, the regulation weapon
until 1842, when it was superseded by the percussion musket. The percussion-cap
is now comparatively little used, as, since the introduction of
cartridges containing their own means of ignition, it is rapidly becoming
a thing of the past. The copper percussion-cap, in the form it still retains,
was invented about 1816, and was universally adopted for sporting-guns
a long time before it was used for the military weapon. In 1842 the percussion
musket was definitely adopted as the weapon of the British army,
but up to that date the flint-locks still continued to be made at Birmingham.
The barrel of the percussion musket then issued was shortly afterwards
rifled, when about the year 1852 the Minié system was adopted, and the
Government awarded to M. Minié, a Frenchman, the sum of £20,000 for
the bullet he had invented. What the meaning of this improvement was
may now be explained, and we must begin by mentioning the various
forms of grooving, or, at least, such forms as found some approval during
the present century, for grooved barrels had been tried long before. At
first the grooves appear to have been intended merely to receive the fouling,
and these were often made without any twist or spiral, but parallel
to the axis of the barrel. The grooves are hollow channels of greater or
less depth, and of various forms; square, triangular, rounded, or of such
a form that the inner line of a section of the barrel would present the form
of a ratchet wheel. The numbers of the grooves made use of have varied
between two and twelve, or more, and different rates of twist, or numbers
of turns of the spiral in the length of the barrel have been resorted to,
181these ranging from half a turn to twelve turns. The Brunswick rifle had
been found wanting in accuracy, when at length in 1846 General Jacobs
proposed the adoption of the conical bullet with projecting spiral ridges
which fitted into grooves cut in the rifle barrel. The difficulty in using
muzzle-loading rifles consisted in the force required to ram down the
bullet, which had to adapt itself to the grooves, and fill them up so that
the gases due to the explosion of the powder should not escape. If the
bullet simply dropped into the bore of the rifle easily, it did not effectually
fill the grooves, which then became channels of this windage, and if, on
the other hand, the leaden bullet was made to fill the grooves from the
muzzle, great force was required, and the time and effort expended in
ramming the missile home, detracted enormously from the efficiency of the
rifle as a military weapon. Mr. Lancaster produced rifles having a slightly
oval, instead of a circular, bore, making, of course, the necessary twist
within the barrel. A bullet of the corresponding section, but nearly
globular, much as if the projecting belt of the Brunswick bullet had been
laterally extended to its opposite poles, could be easily dropped in at the
muzzle, without force being required to make it take grooves, the barrel
being internally smooth throughout. It was, however, soon found that
this easy-fitting ball allowed a considerable amount of windage, and the
Minié system was definitely adopted, in which advantage was taken of a
fact observed some years before by a French artillery officer, who found
that an elongated leaden bullet, if hollowed out at the base, was so expanded
by the pressure of the powder gases that the material was forced
into the grooves of a rifle. Minié made his bullet elongated, pointed in
front, and hollowed out part of its length by a conical
space, the widest part of which was at the base, and was
covered by a small iron cup, that, when driven inwards
by the pressure of the gases, caused an expansion of the
bullet by which the lead was forced into the grooves of
the rifling. But the forces operating on the base of the
bullet would at times cause the iron cup to cut the bullet
in two, and propel the anterior portion only, leaving
the base in the form of a ring clinging to the rifling.
The military authorities had many comparative trials
carried out between the smooth-bore percussion musket
and the Minié rifle. The greater accuracy of the latter
may be inferred from the results of practice made by
men firing at a target 6 feet high and 20 feet broad;
when at 100 yards distance, 74 hits out of 100 shots were made from
the musket, against 94 from the rifle; and the superiority of the latter,
at longer ranges, was increasingly marked. Thus at 260, 300, and 400
yards the respective percentages of hits were for the musket 42, 16, 4½,
but for the same ranges the rifle gave 80, 55, 52.
Fig. 83.—The Minié Bullet.
Curiously enough, the principle of the expanding bullet had been brought
forward by the late Mr. W. Greener seventeen years before the government
prize was awarded to M. Minié. Mr. Greener’s bullets were of an
oval form, being half as long again as their diameter, with one end
flattened where the lead was excavated in a narrowing hollow nearly
through the bullet. In this opening was inserted the end of a tapering
plug of hard metal, and when the rifle was fired this plug was driven home,
and the lead thus expanded took the grooves, so preventing windage, and
giving range and accuracy; while allowing the piece to be loaded with as
182much ease as the smooth-bore musket. The invention, though favourably
reported on by the military authorities at the time, did not receive the
attention it would seem to have deserved. However, in 1857, Mr.
Greener’s claim of priority for the first suggestion of the expanding bullet
was acknowledged by a government award of £1,000.
Fig. 84.—Greener’s Expanding Bullet.
Sir Joseph Whitworth, having been invited by the British military
authorities to institute experiments with a view to producing the best type
of rifle, with the help of the most perfect machinery, constructed the
barrels with a polygonal bore, a plan which he had before adopted
for large guns. The barrels were accurately bored out to a hexagonal
section, and experiments were made to find what number of turns
in the twist would give the projectile a sufficient rapidity of rotation to
maintain it during its flight parallel to its axis. It was found that one
turn in 20 inches was sufficient, and the projectile was made by machinery
to fit accurately but easily into the rifled bore, so that it dropped into its
place, and the loading could be expeditiously performed. The bullet was
long, compared with the bore, which was made smaller than before, and
it was found that the explosion caused it to expand sufficiently to fill up
the corners of the hexagon, so that there was no loss from windage. The
accuracy of aim of the Whitworth rifle was superior to that of any weapon
of the kind that had, up to that time, been produced. When officially
tried against the Enfield, its mean deviation at 500 yards range was only
4½ inches, while that of the Enfield at the same range was 27 inches. Mr.
Whitworth had proved the advantages of using a small bore, an elongated
bullet, and a sharp twist in the rifling; and it was acknowledged that as
a military weapon his rifle was superior to all other arms of similar calibre
that had before been produced. Some doubt appears to have been entertained,
however, as to whether the mechanical perfection of the trial rifles
could be maintained if they came to be manufactured on the large scale,
and also as whether an adequate supply of the polygonal ammunition would
be procurable when required. The Whitworth rifle was never adopted
into the government service, and soon after these trials in 1857, the
adoption of another type of weapon became imperative, as the results obtained
by the Germans with their needle-gun, demonstrated the enormous
advantages of a breech-loading rifle.
Fig. 85.—The Chassepot Rifle.—Section of the Breech.
The French then adopted the Chassepot rifle (so called after its
inventor), which embodied the same principle as the needle-gun, but with
improvements. This arm has a rifled barrel, with a breech mechanism
of great simplicity, which is represented in section in Fig. 85. The
piece marked B corresponds to what is called the “hammer” in the
old lock used with percussion-caps, and the first operation in charging
183the rifle consists in drawing out B, as shown in the cut, until, by the spring,
C, connected with the trigger, A, falling into a notch, the hammer, if we
may so term it, is retained in that position. The effect of this movement
is to draw out also a small rod attached to the hammer, and terminated in
front by a needle, about ½ in. long, at the same time that a spiral spring
surrounding the rod is compressed, the spring being fastened to the front
end of the rod, and abutting against a screw-plug, which closes the hinder
end of F, and permits only the rod to pass through it. The piece F, which
is also movable, has projecting from its front end a little hollow cylinder,
through the centre of which the needle passes, and this little cylinder has
a collar, serving to retain its position, an india-rubber ring surrounding a
portion of the cylinder, and forming a plug to effectually close the rear end
of the barrel. It will be noticed that the cylinder is continued by a smaller
projection, which forms a sheath for the point of the needle. The movable
breech-piece, F, is provided with a short lever, E, by which it is worked.
The second movement performed by the person who is charging the piece
is to turn this lever from a horizontal to a vertical position, which thus
causes the piece F to turn 90° about its axis, and then by drawing the lever
towards him he removes the piece F from the end of the barrel, which, thus
exposed, is ready to receive the cartridge. The cartridge contains the powder
and the bullet in one case, the posterior portion containing also a charge
of fulminate in the centre, and it is by the needle penetrating the case of
the cartridge and detonating this fulminate that the charge is exploded.
When the cartridge has been placed in the barrel, the piece F is pushed
forward, the metallic collar and india-rubber ring stop up the rear of the
barrel, and on turning the lever, E, into a horizontal position, the breech
is entirely closed. If now the trigger be drawn, the hammer is released,
and the spring carries it forward, at the same time impelling the needle
through the base of the cartridge-case, where it immediately causes the
explosion of the fulminate. The bullet is conical, and its base having a
slight enlargement, the latter moulds itself to the grooves with which the
barrel is rifled. When the piece has not to be fired immediately, the lever
is not placed horizontally, but in an inclined position, in which the hammer
184cannot move forward, even if the trigger be drawn. The Chassepot has an
effective range of 1,093 yards, and the projectile leaves the piece with a
velocity of 1,345 ft. per second, the trajectory being such that at 230 yards
the bullet is only 18 in. above the straight line. The piece can be charged
and fired by the soldier in any position, and it was found that it could be
discharged from seven to ten times per minute, even when aim was taken
through the sights with which it is furnished, and fourteen or fifteen times
per minute without sighting. The ordinary rifled musket, which this arm
superseded, could only be fired twice in a minute, and could only be loaded
when the soldier was standing up.
Other nations followed either by adopting as their infantry arm some
form of breech-loader, or by converting their muzzle-loaders into breech-loaders
as a temporary expedient, pending the selection of some more
perfect type. When in 1864 a committee which had been appointed to
investigate the question of proper arms for our infantry, recommended
that that branch of the service should be supplied with breech-loaders,
our Government, considering that no form of breech-loader had up to
that time been invented which would unequivocally meet all the requirements
of the case, wisely determined that, pending the selection of a
suitable arm, the service muzzle-loaders should meanwhile be converted
into breech-loaders. The problem of how this was to be done was solved
by the gunmaker Snider, and in the “Converted Enfield” or “Snider” the
British army was provided for a time with an arm satisfying the requirements
of that period. This change of weapon was effected at a comparatively
small outlay, for the conversion cost less than twenty shillings
an arm. The breech action in the Snider consisted of a solid piece of
metal which closed the breech end of the barrel, and, being hinged on
the right-hand side parallel to the barrel, could be turned aside, making
room for the insertion into the conically widened bore of a metallic
cartridge case, invented by Colonel Boxer, which contained the projectile,
the powder charge, and the means of ignition in itself. A short backward
movement of the breech-lock caused a claw acting on the base of the
spent cartridge case to withdraw it from the barrel, and then the reaction
of a spring brought the breech-block back into position, after insertion
of a new cartridge. This cartridge proved very effective in increasing
the range and accuracy of the weapon. It should be mentioned that all
the breech-loading mechanisms are provided with arrangements by which
the metallic cases of the spent cartridges are automatically extracted
from the barrel. The authorities having, in 1866, offered gunmakers and
others handsome prizes for the production of rifles best fulfilling certain
conditions, nine weapons were selected out of 104 as worthy to compete.
No first prize was awarded, but the second was given to Mr. Henry,
while Mr. Martini was seventh on the list. In order to obtain a weapon
fulfilling all the requirements, a vast number of experiments were made
by the committee appointed for that purpose, as to best construction of
barrel, size of bore, system of rifling, kind of cartridge, and other particulars,
and assistance was rendered by several eminent gunsmiths and
engineers.
Fig. 86.—Section of Martini-Henry Lock.
After a severe competition it appeared that the best weapon would be
produced by combining Henry’s system of rifling with Martini’s mechanism
for breech-loading. The parts constituting the lock and the mechanism for
working the breech, shown in Fig. 86, are contained in a metal case, to which
is attached the woodwork of the stock, now constructed in two parts. To this
185case is attached the butt of the rifle by a strong metal bolt 6 in. in length,
A, which is inserted through a hole in the heel-plate. The part that closes
the breech—termed the “block”—is marked B. It turns loosely on a pin,
C, passing through its rear end and fixed into the case at a level somewhat
higher than the axis of the barrel. The end of the block is rounded
off so as to form with the rear end of the case, D, which is hollowed out to
receive it in a perfect knuckle joint. Let it be observed that this rounded
surface, which is the width of the block, receives the whole force of the
recoil, no strain being put on the pin, C, on which the block turns. In the
experiments a leaden pin was substituted, and the action of the mechanism
was not in the least impaired. This arrangement serves greatly to diminish
the wear and the possibility of damage from the recoil. As the pin on
which the block turns is slightly above the axis at the barrel, it follows that
the block, when not supported, immediately drops down below the barrel.
Behind the trigger-guard is a lever, E, working on a pin, F, fitted into the
lower part of the case. To this lever is attached a much shorter piece
called the “tumbler,” which projects into the case, G. It is this tumbler
which acts as a support for the block, and raises it into its firing position
or lowers it according as the lever, E, is drawn toward a firer or pushed
forward. How this is accomplished will be readily understood by observing
the form of the notch, H, in which the upper end of the tumbler moves.
It will be noticed that the piece being in the position for firing, if the
lever be pushed back, G slides away from the shallower part of the notch
into the deeper, and the block accordingly falls into the position shown in
the figure; and if again the lever is drawn backward, G acting on H will
raise the block to its former position. The block or breech-piece is hollowed
out on its upper surface, I, so as to permit the cartridge to be readily inserted
into the exploding chamber, J. The centre of the block is bored
out, and contains within the vital mechanism for exploding the cartridge,
namely, a spiral spring, of which the little marks at K are the coils in
section. These coils pass round apiece of metal called the “striker,”
which is armed with a point, capable of passing through a hole in the front
186face of the block exactly behind the percussion-cap of the cartridge when
the block is in the firing position. When the lever handle is moved forward,
it causes the tumbler, which works on the same pin, to revolve, and
one of its arms draws back the striker, compressing the spring in so doing,
so that as the block drops down the point of the striker is drawn inwards.
In this position the piece receives the cartridge into the chamber. The
lever, E, being now drawn backward, the piece is forced into the notch, H,
and the block is kept firmly in its place; besides this, there is a further
compression of the spring by the tumbler, and in this position the spring
is retained by the rest-piece, L, which is pushed into a bend in the tumbler.
By pulling the trigger this piece is released, so that the tumbler can revolve
freely, and relieve the pent-up spring, whose elasticity impels the striker
forward, so that this enters the carriage directly. A very important and
ingenious part of this arrangement is the contrivance for extracting the
case of the exploded cartridge. The extractor turns on the pin, M, and
has two arms pointing upwards, N, which are pressed by the rim of the
cartridge pushed home into two grooves cut in the sides of the barrel. It
has another arm, O, bent only slightly upwards and pointing towards the
centre of the case, and forming an angle of about 80° with the above-mentioned
upright arm; when, by pushing forward the lever, its short
arm drops into the recess, the block, no longer supported, falls, and hits
the point of the bent arm of extractor, so causing the two upright arms to
extract the cartridge-case a little way.
Fig. 87.—The Martini-Henry Rifle.
A, ready for loading; B, loaded and ready for firing.
The barrel is of steel; the calibre is 0·451 in. It is rifled on Mr. Henry’s
patent system. The section of the bore may be generally described as a
heptagon with re-entering angles at the junctions of the planes, so that
there are fourteen points of contact for the bullet, viz., one in the middle
of each plane, and one at each of the re-entering angles. The twist of
rifling is one turn in 22 in. The charge consists of 85 grains of powder,
and a bullet weighing 480 grains, of a form designed by Mr. Henry. The
cartridge is of the same general construction as the “Boxer” cartridge,
used in the Snider rifle, but it is bottle-shaped, the diameter being enlarged
from a short distance in rear of the bullet, in order to admit of its
being made shorter, and consequently stronger, than would be otherwise
possible. A wad of bees’-wax is placed between the bullet and powder, by
187which the barrel is lubricated at each discharge. The sword-bayonet to
be used with this rifle is of a pattern proposed by Lord Elcho. It is a
short sword, broad towards the point, and furnished on a portion of the
back with a double row of teeth, so as to form a stout saw. It is so balanced
as to form a powerful chopping implement, so that, in addition to its primary
use as a bayonet, it will be useful for cutting and sawing brushwood,
small trees, &c.
The following are the principal particulars of weight, dimensions, &c., of
the Martini-Henry rifle:
Without bayonet
4
ft.
1
in.
Length of rifle
With bayonet fixed
5
ft.
8
in.
Of barrel
2
ft.
9·22
in.
Calibre
0·451
in.
Rifling
Grooves
7
Twist
1
turn in
22
in.
Weight
Without bayonet
8
lbs.
7
oz.
With bayonet
10
lbs.
4
oz.
Bayonet
Length
2
ft.
1½
in.
Weight without scabbard
1
lb.
8
oz.
Charge of powder
85
grains.
Weight of bullet
480
grains.
The rifle is sighted to 1,400 yards.
As an evidence of the accuracy of fire in this rifle, it may be stated that
of twenty shots fired at 1,200 yards, the mean absolute deflection of the
hits from the centre of the group was 2·28 ft. The highest point in the
trajectory at 500 yards is rather over 8 ft. so that the bullet would not pass
over a cavalry soldier’s head within that distance. The trajectory of the
Snider at the same range rises to nearly 12 ft. The bullet will pass through
from thirteen to seventeen ½ in. elm planks placed 1 in. apart at 20 yards
distance; the number pierced by the Snider under similar circumstances
being from seven to nine. As regards rapidity of fire, twenty rounds have
been fired in 53 seconds; and one arm which had been exposed to rain and
water artificially applied for seven days and nights, and had during that
time fired 400 rounds, was then fired, without cleaning, twenty rounds in
1 minute 3 seconds.
Rifles of the Martini-Henry and Chassepot type were soon superseded,
for as early as 1876 Switzerland had armed her troops with a magazine
rifle of a smaller calibre than any then in use, and this weapon was found
so effective that in a few years after every European nation had followed
suit, as also had the United States and Japan, each country adopting
some particular pattern of a weapon with certain modifications. Of these
the Mannlicher and the Mauser are much used. A magazine rifle is one
that can be fired several times successively without reloading. Like
revolvers, the magazine arms repeat their fire, but instead of having
several distinct firing chambers, they have but one, from which the empty
cartridge cases are automatically extracted by the breech mechanism, for
the magazine rifle is necessarily a breech-loader. The magazine rifle
carries a supply of cartridges, which one after another are brought into
the firing chamber by the simple action of the breech mechanism, so that
the soldier is enabled to discharge several rounds in any position without
reloading. The several varieties of the magazine rifle may be classed
188according to the position of the magazine. This may be: First, in the
stock; second, under the barrel; third, in a box under the breech; or
fourth, in a box above the breech. In the first and second variety the
cartridges are in line in a tube, out of which they are moved on by a spiral
spring, and this was the earlier form of the weapon. The box above or
below the breech is the later development, and has the
advantage of holding the cartridges lying side by side,
and thus in a position in which they are not so liable to
injure each other as in the tubular arrangements. Then,
again, the movement of the cartridge in the breechbox
in arriving at the firing chamber is much less than in the
linear magazines, and the centre of gravity of the whole
changes but little when the supply is exhausted. With
any of the varieties of magazine a suitable modification
of the mechanism may be adopted, so that the weapon
can at will be used as a single firing rifle, but changeable
in an instant to the magazine form. Again, the box
magazine may be made as a fixture on the rifle, or it may
be detachable. Commissions of military authorities had
for several years been deliberating upon the best models
for their respective nations, while Professor Hebler was
working out his researches as to the best calibre for
military rifles. Hebler published a work showing the
great advantages of a bore one-third less in diameter
than that commonly in use, which was about 0·45 inch,
as in our Martini-Henry. The small-calibre rifle shoots
straighter and hits harder than the large bore one, and
the recoil is less, and so is the weight of the weapon.
Lead is found to be too soft a material for the bullet of
the small-bore rifles, as it does not keep in the rifling,
which has a sharper turn than that in the older weapon;
hence the bullets are now cased in steel or nickel. These
bullets have remarkable power of penetration. Some
will go through a steel plate 1¼ inch thick, making a clean
hole in it, and the Lebel bullet penetrates 15 inches of
solid oak, at a distance of 220 yards. Such a missile
would, therefore, be capable of going completely through
the bodies of several men or horses.
Fig. 88.—The Mannlicher Magazine Rifle.
The Germans, about 1888, adopted a magazine rifle
known as the Mauser. It had a fixed tubular magazine
for eight rounds below the barrel, and a breech mechanism
of the Remington-Keene type. The French followed suit
with their famous Lebel gun, the construction of which
was long kept secret. It also has a fixed under barrel
tubular magazine, and the cartridges used with it contain
smokeless powder. It is said that a new gun of practically
the same pattern has been adopted by Russia, but with a detachable
magazine to contain five rounds. The Russian gun will also use smokeless
powder. In England, a small-bore rifle of 0·303 inches calibre is
now issued to all troops. It has an under breechbox magazine, modified
from the Lee rifle. The box is detachable, so that the weapon could
normally be used as a single loader, and the magazine attached only
when required. But the British authorities have decided that the
189magazine box is to be attached to the weapon by a chain. The first
issue of this pattern of rifle to British soldiers took place early in 1890.
The Austrians are adopting the Mannlicher pattern, in which the
magazine idea is embodied in a complete and practical form. This rifle
has a fixed box magazine below the breech. From this box, in which
the cartridges—five in number—lie side by side, they are fed up by
springs as they are disposed of by the movement of the breech mechanism.
The magazine is recharged by placing in it a tin case containing five
cartridges, and the case drops out when all the cartridges have been fired.
In this form there is of course no necessity for providing any mechanism
for holding the magazine in reserve while the rifle is used as a single loader.
As to calibre, the Austrian authorities follow other countries in adopting
a small bore, namely, 0·315 inch. Italy has converted her single-fire
Vetterli rifle into a magazine arm, with a box something like the Mannlicher,
and Belgium has adopted a gun of the same type. The rate of
fire from charged magazines of such guns as the “Lee,” “Mannlicher”
and “Vetterli,” worked with the right hand without bringing the piece
down from the shoulder is, for all of them, about one shot per second;
but the time that is required to recharge the magazines varies much
according to the contrivance used. The number of rounds the magazine
of a rifle is capable of containing when fully charged is from 5 to 12, or
more, according to the difference of system. It is considered that in the
detachable Lee or the quick recharging Mannlicher five rounds are
ample for use at a critical moment.
Fig. 89.—The Magazine and Breech of the Mannlicher Rifle.
The calibre of the military rifle has been decreased with almost every
new pattern adopted. Thus, while the old “Brown Bess” had a calibre
of 0·75 inch, in the last issue of it the bore was reduced to 0·693 inch; the
Enfield (1852) had a bore of 0·577 inch; the Martini-Henry, 0·451 inch,
which, in a newer pattern adopted in 1887, was reduced to 0·400 inch;
and, finally, in the Lee-Metford, the calibre is only 0·303 inch. A similar
consecutive reduction of bores has taken place in the rifles adopted by
other countries, and one of the latest type, issued for the use of the
United States Navy, has a bore of only 0·236 inch, and it is even expected
that a still smaller one will become general. The advantage of the narrow
and lighter projectile is that while it has a higher initial velocity with a
given charge, its flight is less checked by the resistance of the atmosphere,
the section it presents being so much less. Thus the bullet of 0·236 inch
diameter has a section little more than one-fourth that of the 0·45 inch
190bullet. The difference is well shown in the comparative heights of the
trajectory (or path of the bullet) of the Martini-Henry 0·450 inch bullet,
and that of the 0·303 inch Lee-Metford (the latter with cordite ammunition);
for at a range of 1,000 yards the former reaches to 48 feet above
the line of sight, while the latter rises to only 25 feet.
Some form of repeating or magazine rifle has now been adopted by all
the most important nations of the world. The number of shots contained
in the magazines varies from 5 to 12. In the British detachable box
magazine there are ten charges. The calibres of the barrels range in the
infantry patterns of different nations from 0·256 inch to 0·315 inch; the
explosive used in every case is some kind of smokeless powder, and this,
in the cartridge for the Lee-Metford, is cordite. The bullets are not made
simply of lead, but of lead coated with a harder metal or alloy such as
steel, cupro-nickel, nickel steel, or they consist entirely of some of these
alloys.
Although the magazine rifle is now the regulation weapon of the infantry
of all great armies, it is not improbable that at no distant future it maybe
superseded by one in which, as in certain machine guns, the force of the
recoil will be used for actuating the breech and lock movements. Many
patents have already been taken out for rifles on this principle, and several
patterns have actually been constructed, in which a merely momentary
contact of the breech-piece with the end of the barrel is sufficient; the recoil
of the barrel with the reaction of a spring performs all the requisite
movements with such rapidity that an amazing speed of firing has been
obtained. It is said that such an automatic gun can send forth bullets at
a perfectly amazing rate. Of course the mechanism of such a gun
is somewhat intricate, and it is impossible to explain its construction and
action without a great number of diagrams and much description.
Having briefly sketched in the foregoing section the development of
the military rifle from such weapons as our own “Brown Bess,”
down to the repeating or magazine rifle, we now purpose to adopt a
similar course with regard to ordnance, giving also some particulars of
the methods of manufacture, etc., and following in general the order of
history.
Naturally there is nothing that accelerates progress in warlike inventions
so much as the exigences of war itself. This is well exemplified
in circumstances attending the Crimean War, which was waged in 1854
by England and France in alliance against Russia. The desire of having
ships that could run the gauntlet of the heavy guns mounted on Russian
forts led to the construction of La Gloire and other armour-plated
vessels, as we have already seen, and a suggestion of the French
Emperor, as to improving metal for guns, made to Mr. Bessemer, led
incidentally but ultimately to the great revolution in the manufacture of
steel, although it is true that Krupp of Essen had begun to produce
small cast-steel ordnance as early as 1847. But what determined the
necessity for rifled ordnance was more particularly the greater comparative
effects obtained by the muzzle-loading rifles over the field artillery
191then in use in the several engagements that took place in the Crimea,
especially in the battle of Inkerman (1854). The rifles so much surpassed
in accuracy at long ranges the smooth-bore field-pieces firing spherical
projectiles, that field artillery was on the point of losing its relative
importance, and even in the matter of range the latter lost so much by
windage that the men serving the artillery could sometimes be leisurely
picked off by the rifle sharp-shooters. Inventors were soon at work on
devising methods of increasing the accuracy of ordnance fire with both
light and heavy pieces, and before the end of the war some cast-iron
guns rifled on Lancaster’s plan had been mounted on forts and in ships,
without proving very successful except in regard to increase of range
when elongated pointed projectiles were used with them.
Fig. 90.—32–pounder, 1807.
Now let us see of what kind was the ordnance used for some years
after the middle of the century, in order that we may be the better able
to appreciate the progress that has since been made. Ordnance is, as
already noticed, of several species, as guns mounted on fortresses, naval
guns, siege guns, field-guns, etc., and the size of the pieces under each of
those heads is distinguished sometimes in one, sometimes in another of
three different ways. We may name it by the weight of the gun itself
in tons or hundredweights, as “a 35–ton gun,” etc.; or by the weight
of its projectile, as “a 68–pounder,” etc.; or by its calibre, that is the
diameter of its bore, as “a 4–inch gun,” etc. We may take the naval
guns with which Nelson won his battles (Trafalgar, 1807) as representative
of all except field ordnance up to about 1856. They were all made
of cast iron, threw spherical projectiles, and were very rudely mounted.
The gun most commonly mounted on board our ships of war was the
32–pounder, weighing 32 cwt., shown with its carriage in Fig. 90. The
carriage was of wood, and consisted of two side pieces joined back and
front by two transverse pieces and carried by four low wooden wheels. The
trunnions of the gun fitted into bearings at the top of the side-pieces, and
were secured by iron plates that passed over them in a semi-cylindrical
form and were bolted down to the wood. The position of the trunnions
on the gun was always such that the breech end of the gun preponderated,
being supported on an adjustable wooden wedge; and when the
muzzle of the gun had to be lowered, this was done by raising the breech
end with handspikes and pushing in the wedge so far as to prevent the
192breech from dropping down again. There was a vent or narrow passage
to contain a train of powder from the touch-hole at the upper part of the
breech to the rear of the charge. When the gun was fired, with its muzzle
protruding a little way out of the port-hole, the recoil would trundle it
inwards about its own length, when its course would be stayed by a thick
rope attached to the sides of the vessel; and by other tackle it would be
kept in position until loaded, when it would be allowed to roll back, or
would be drawn by ropes and pulleys out to the port-hole, and by the
same means such lateral inclination as might be required could be given.
This last adjustment was called training the gun. A 32–pounder required
the services altogether of a dozen or fourteen men, but these by virtue of
constant drill would learn to handle the clumsy machine with a certain
amount of expedition. If we except a notch on the highest point of the
muzzle, the pieces were devoid of anything of the nature of sights, though
sometimes marks were made on the adjustable wedge under the breech
to correspond with certain elevations. Nor were sights required; for the
mode of fighting then was to get quite close to the adversary’s ship and
pour in a broadside by firing simultaneously all guns on the enemy’s side
when they had been trained (by rough methods), so as to concentrate
their effect as much as possible on one point of the antagonist. Nelson’s
famous ship the Victory carried a few larger guns than the 32–pounders,
namely, two 68–pounders, called carronades (from having first been cast
at Carron in Scotland), and some 42–pounders. The 32– and 42–pounders
numbered together thirty, and there were also as many 24–pounders, with
forty 12–pounders. These were all simply cast of the required dimensions,
and were not made with the one single improvement which after two
centuries’ use of cast-iron guns had been introduced into France about
fifty years before, namely, the boring of the chase out of a solid casting.
On the outbreak of the Crimean War (1854) the minds of many inventors
were occupied by the problem of ordnance construction, and this also
engaged the attention among others of two of the most eminent British
mechanical engineers of the day. These were Sir W. Armstrong and Sir
J. Whitworth, who, with others, were invited by our War Department
to submit the best models of field and heavy guns their skill was severally
able to produce. Two years afterward, Sir W. Armstrong had, after
many experiments, completed a gun of 1·88 in. calibre. This had a
forged steel barrel 6 feet in length; but it was only after eight such
forgings had been bored and rejected on account of flaws revealed only
by the boring that a sound barrel was at length obtained. This barrel
was strengthened on the outside by jackets made from coils of wrought
iron bars welded into a piece and shrunk on while hot (of which process
we shall have something more to say presently); the barrel was rifled with
many shallow grooves, and the pointed projectile, 3 calibres long, was
made of lead, for which afterwards iron coated with lead was substituted.
This gun was a breech-loader, the breech being closed by a block let into
a slot after loading, and then pressed against the barrel by some turns of
a screw which advanced parallel to the axis of the piece, and was made
hollow for loading through, before the closing block was put in. In a
trial of the various pieces ready in 1857, it was found that the Armstrong
gun made as just described had an accuracy and range immensely
greater than any weapon that had ever been tested, and the Government
authorities approved of the system of construction, except that they
preferred muzzle-loading pieces to breech-loading, as being simpler in
193action, more easily kept in repair, and cheaper in original cost and
ammunition.
When Sir Joseph Whitworth’s gun was, in 1863, submitted to a competitive
trial against the Armstrong, as to their endurance and mode of
ultimate failure when fired with ever-increasing charges of powder and
shot, at the forty-second round the Armstrong breech-loader split, and at
the sixtieth the Armstrong muzzle-loader had one of its coils cracked;
while it was not until the ninety-second round that the Whitworth gun
burst violently into eleven pieces. These competing guns were 12–pounder
field-guns weighing 8 cwts., and from each 2,800 regulation rounds had
been fired before they were subjected to the bursting proofs. The result
of these trials being that the authorities considered that steel was not
then sufficiently reliable, and they decided to adopt the system of building
up rifled guns with iron jackets over an inner tube of steel. Sir
Joseph Whitworth made his guns entirely of steel, and they were striking
examples of beautiful and accurate workmanship. His system of rifling
consisted in forming the bore of the gun so that its section is a regular
hexagon, and the projectile is an elongated bolt with sides exactly fitting
the barrel of the gun: the projectile is, in fact, a twisted hexagonal
prism. Fig. 91 shows at the left-hand side the section of the barrel,
and on the right we see the form of the projectile on a smaller scale, this
last representing, in fact, the exact size and shape of the bullet of the
Whitworth rifle mentioned on another page. Sir Joseph’s guns were
muzzle-loaders, and they were remarkable for their long range and
accuracy of fire. One of these guns, with a charge of 50 lbs. of gunpowder,
threw a 250–lb. shot a distance of nearly six miles, and on another occasion
a 310–lb. shell was hurled through the air, and first touched the ground
at a distance of more than six and a quarter miles from the gun. These
distances are greater than any to which shot or shell had previously been
thrown.
Fig. 91.—Whitworth Rifling and Projectile.
As the material of these Whitworth guns was very costly, and very
perfect workmanship was required in the formation of the barrel and the
shots, the expense attending their manufacture and use was much greater
than that incurred in the case of the Armstrong guns. Sir W. Armstrong’s
194estimate for a 35–ton gun was £3,500, and Sir J. Whitworth’s, £6,000.
The gun, as constructed at Woolwich on Mr. Fraser’s plan, was estimated
to cost £2,500. The first cost of a gun is a matter for consideration,
since each piece, even the strongest, is able only to fire a limited number
of rounds before it becomes unsafe or useless. It appears that no cannon
has yet been constructed capable of withstanding without alteration
the tremendous shocks given by the explosion of the gunpowder, and
these alterations, however small at any one discharge, are summed up
and ultimately bring to an end what may be termed the “life of the
piece.”
About the year 1858 Sir William Armstrong (afterwards Lord Armstrong)
established at Elswick, Newcastle-on-Tyne, a manufactory of
ordnance, which has since developed into the great arsenal now so well
known all over the world. Here all the resources of science have been
applied to the problems of artillery, and experiments carried on with a
prodigality of cost and promptness of execution impossible at a government
establishment trammelled with official regulations. Here, and also
at Woolwich, our national ordnance factory, guns have since always been
constructed on the building-up plan advocated by Sir W. Armstrong,
whose principle consists in disposing of the fibre of the iron so as best to
resist the strains in the several parts of the gun. Wrought iron being fibrous
in its texture has, like wood, much more strength in the direction of the grain
than across it. The direction of the fibre in a bar of wrought iron is parallel
to its length, and in that direction the iron is nearly twice as strong as it is
transversely. A gun may give way either by the bursting of the barrel or
by the blowing out of the breech. The force which tends to produce the
first effect acts transversely to the axis of the gun; hence the best way to
resist it is to wrap the iron round the barrel, so that the fibres of the metal
encircle it like the hoops of a cask. The force which tends to blow out the
breech is best resisted by disposing the fibres of the iron so as to be parallel
to the axis of the gun; hence Sir W. Armstrong makes the breech-piece
from a solid forging with the fibre in the required direction. But the
195Elswick building-up principle involves much more than the direction of
the fibres of the iron, for each coil or jacket, after having its spires welded
together, was bored out on a lathe, and the exterior of the part of the gun
on which it was to be placed was also turned with the utmost exactness,
so that when the enveloping piece was heated to a certain temperature
and in this state brought into position, it would in cooling compress the
parts it encircled just to that degree which careful calculations showed
would best strengthen the gun without unduly straining the metal at any
part. The Elswick guns being built up of several superimposed jackets
of calculated lengths and thicknesses, the means was afforded of distributing
the tensions throughout the whole mass of metal to the best
advantage. In the simpler form, arranged by Mr. Fraser, and for the
sake of economy adopted by the authorities at Woolwich in 1867, the
greater part of the benefit derivable from adjustment of tension was no
doubt sacrificed to cheapness of manufacture. These, and also the forms
of Armstrong guns that have not yet been described, ceased to be made
after 1880, by which time steel had replaced iron in every part of the
construction and fittings of guns, and muzzle-loading had been definitely
abandoned in favour of breech-loading.
Fig. 93.—35–ton Fraser Gun.
Now, in 1874, when the first edition of the present work was in
preparation, the Fraser-Woolwich guns were in full vogue, being spoken
of by the public press as the ne plus ultra of artillery construction in
size, efficiency, and economy. When, accordingly, the author had been
privileged to visit the arsenal and witness the production of these guns
in every stage of their manufacture, he wrote a description of it which is
here retained as printed at the time, seeing that it may not be without
historical interest, particularly since great numbers of these guns must
still be extant, mounted on our forts in various parts of the world, and
seeing also that the description of the simpler formations may render
more easily to be understood future references to similar operations in
gun-making as have been retained in the later developments. Of course,
the following description was written in the present tense, and therefore in
perusing it the reader must constantly bear in mind that the guns with
196which our ships of war have since been equipped are in every respect
entirely different from
Fig. 94.—Section of 9 in. Fraser Gun.
Until the year 1867 the guns made at Woolwich were constructed according
to the original plan proposed by Sir W. Armstrong, and on this system
one of the large guns consisted of as many as thirteen separate pieces.
These guns, though unexceptionable as to strength and efficiency, were
necessarily so very costly that it became a question whether anything could
be done to lessen the expense by a simpler mode of construction or by
greater economy in the material. The problem was solved in the most
satisfactory manner by Mr. Fraser, of the Royal Gun Factory, who proposed
an important modification of the original plan, and the adoption of
a kind of iron cheaper than had been previously employed, yet perfectly
suited for the purpose. Mr. Fraser’s modification consisted in building up
the guns from only a few coils, instead of several, the coils being longer
than Sir W. Armstrong’s, and the iron coiled upon itself two or even three
times: a plan which enabled him to supersede the breech-piece, formerly
made in one large forging, by a piece formed of coils. In order to perceive
the increased simplicity of construction introduced by Mr. Fraser, we need
but glance at the section of a 9 in. gun constructed according to his system,
Fig. 94, and remember that a piece of the same size made after the original
plan had ten distinct parts, whereas the Fraser is seen to have but four. Compare
also Figs. 92 and 93. We shall now describe the process of making the
Fraser 9 in. gun. The parts of the gun as shown in the section, Fig. 94, are:
1, the steel barrel; 2, the B tube; 3, the breech-coil; 4, the cascable screw.
The inner steel barrel is made from a solid cylinder of steel, which is
supplied by Messrs. Firth, of Sheffield. This steel is forged from a cast
block, the casting being necessary in order to obtain a uniform mass, while
the subsequent forging imparts to it greater solidity and elasticity. After
the cylinder has been examined, and the suitable character of the steel
tested by trials with portions cut from it, the block is roughly turned and
bored, and is then ready for the toughening process. This consists in heating
the tube several hours to a certain temperature in an upright furnace,
and then suddenly plunging it into oil, in which it is allowed to remain for a
day. By this treatment the tenacity of the metal is marvellously increased.
197A bar of the steel 1 in. square previous to this process, if subjected to a
pull equal to the weight of 13 tons, begins to stretch and will not again
recover its original form when the tension is removed, and when a force of
31 tons is applied it breaks. But the forces required to affect the toughened
steel in a similar manner are 31 tons and 50 tons respectively. The
process, unfortunately, is not without some disadvantages, for the barrel is
liable to become slightly distorted and even superficially cracked. Such
cracks are removed by again turning and boring; the hardness the steel
acquires by the toughening process being shown by the fact that in the
first boring 8¼ in. diameter of solid steel is cut out in 56 hours, yet for
this slight boring, in which merely a thin layer is peeled off, 25 hours are
required; and lest there should be any fissures in the metal, which, though
not visible to the eye, might make the barrel unsound, it is filled with
water, which is subjected to a pressure of 8,000 lbs. per square inch. If
under this enormous pressure no water is forced outwards, the barrel is
considered safe. It is now ready to have the B tube shrunk on it.
The B tube, like certain other portions of these guns, is constructed from
coiled iron bars, and this constitutes one great peculiarity of Sir W. Armstrong’s
system. It has the immense advantage of disposing the metal so
that its fibres encircle the piece, thus applying the strength of the iron in
the most effective way. The bars from which the coils are prepared are
made from “scrap” iron, such as old nails, horse-shoes, &c. A pile of such
fragments, built up on a wooden framework, is placed in a furnace and
intensely heated. When withdrawn the scraps have by semi-fusion become
coherent, and under the steam hammer are soon welded into a compact
mass of wrought iron, roughly shaped as a square prism. The glowing
mass is now introduced into the rolling-mill, and in a few minutes it is
rolled out, as if it were so much dough, into a long bar of iron. In order to
form this into a coil it is placed in a very long furnace, where it can be
heated its entire length. When sufficiently heated, one end of the bar is
seized and attached to an iron core of the required diameter, and the core
being made to revolve by a steam engine, the bar is drawn out of the furnace,
winding round the core in a close spiral, so that the turns are in contact.
The coil is again intensely heated, and in this condition a few strokes
of the steam hammer in the direction of its axis suffice to combine the
spires of the coil into one mass, thus forming a hollow cylinder.
The B tube for the 9 in. gun is formed of two double coils. When the
two portions have been completely welded together under the steam
hammer, the tube, after cooling, is roughly turned and bored. It is again
fine bored to the required diameter, and a register of the diameter every
few inches down the bore is made. These measurements are taken for the
purpose of adapting most accurately the dimensions of the steel barrel to
the bore of the B tube, as it is found that perfect exactness is more easily
obtained in turning than in boring. The steel barrel is therefore again
turned to a size slightly larger than the bore of the B tube, and is then
placed muzzle end upwards, and so arranged that a stream of water, to
keep it cool, shall pass into it and out again at the muzzle, by means of a
syphon, while the B tube, which has been heated until it is sufficiently
expanded, is passed over it and gradually cooled.
If now the B tube were allowed to cool spontaneously, its ends would, by
cooling more rapidly than the central part, contract upon the steel barrel
and grip it firmly at points which the subsequent cooling would tend to
draw nearer together longitudinally, and thus the barrel would be subjected
198to injurious strains. In order to prevent this, the B tube is made to cool
progressively from the breech end, by means of jets of water made to fall
upon it, and gradually raised towards the muzzle end, which has in the
meanwhile been prevented from shrinking by having circles of gas-flames
playing upon it.
The breech-coil, or jacket, is formed of three pieces welded together.
First, there is a triple coil made of bars 4 in. square, the middle one being
coiled in the reverse direction to the other two. After having been intensely
heated in a furnace for ten hours, a few blows on its end from a powerful
steam hammer welds its coils perpendicularly, and when a solid core has
been introduced, and the mass has been well hammered on the sides, it
becomes a compact cylinder of wrought iron, with the fibres all running
round it. When cold it is placed in the lathe, and the muzzle end is
turned down, leaving a shoulder to receive the trunnion-ring. The C coil
is double, welded in a similar manner to the B coil, and it has a portion
turned off, so that it may be enclosed by the trunnion-ring.
The trunnion-ring is made by punching a hole in a slab of heated iron
first by a small conical mandrel, and then enlarging by repeating the process
with larger and larger mandrels. The iron is heated for each operation,
and the trunnions are at the same time hammered on and roughly shaped—or,
rather, only one has to be hammered on—for a portion of the bar
which serves to hold the mass forms the other. The trunnion-ring is then
bored out, and after having been heated to redness, is dropped on to the
triple breech-coil which is placed muzzle end up, and the turned end of the
C coil (of course, not heated) is then immediately placed within the upper
part of the trunnion-ring. The latter in cooling contracts so forcibly as to
bind the ends of the coils together, and the whole can thus be placed in a
furnace and heated to a high temperature, so that when removed and put
under the steam hammer, its parts are readily wielded into one mass. The
breech-coil in this state weighs about 16 tons; but so much metal is removed
by the subsequent turnings and borings, that it is reduced to nearly
half that weight in the gun. It is then turned in a lathe of the most massive
construction, which weighs more than 100 tons. Fig. 34, page 95, is
from a drawing taken at Woolwich, and shows one of the large guns in the
lathe. No one who witnesses this operation can fail to be struck with the
apparent ease with which this powerful tool removes thick flakes of metal
as if it were so much cheese. The projections of the trunnions prevent the
part in which they are situated from being finished in this lathe, and the
gun has to be placed in another machine, where the superfluous metal of
the trunnion-ring is pared off by a tool moving parallel to the axis of the
piece. Another machine accomplishes the turning of the trunnions, the
“jacket” being made to revolve about their axis. The jacket is then accurately
bored out with an enlargement or socket to receive the end of the
B tube, and a hollow screw is cut at the breech end for the cascable.
The portion of the gun, consisting of the steel barrel with the B tube
shrunk on it, having been placed upright with the muzzle downwards, the
breech-piece, strongly heated, is brought over it by a travelling crane, and
slips over the steel barrel, while the recess in it receives the end of the B
tube. Cold water is forced up into the inside of the barrel in order to keep
it cool. As the breech cools, which it is allowed to do spontaneously, it
contracts and grips the barrel and B tube with great force. The cascable
requires to be very carefully fitted. It is this piece which plays so important
a part in resisting the force tending to blow out the end of the barrel. The
199cascable is a solid screw formed of the very best iron, and its inner end is
wrought by scraping and filing, so that when screwed in there may be perfect
contact between its face and the end of the steel barrel. A small
annular space is left at the circumference of the inner end, communicating
through a small opening with the outside. The object of this is, that in
case of rupture of the steel barrel, the gases escaping through it may give
timely warning of the state of the piece.
Besides minor operations, there remain the important processes of finishing
the boring, and of rifling. The boring is effected in two operations,
and after that the interior is gauged in every part, and “lapping” is resorted
to where required, in order to obtain the perfect form. Lapping consists
in wearing down the steel by friction against fine emery powder and oil,
spread on a leaden surface. The piece is then ready for rifling. The
machinery by which the rifling is performed cannot be surpassed for its
admirable ingenuity and simplicity.
In this operation the gun is fixed horizontally, its axis coinciding with
that of the bar, which carries the grooving tools. This bar is capable of two
independent movements, one backwards and forwards in a straight line in
the direction of the length of the bar, and the other a rotation round its axis.
The former is communicated by a screw parallel to the bar, and working
in a nut attached to the end of it. For the rotatory movement the bar
carries a pinion, which is engaged by a rack placed horizontally and perpendicularly
to the bar, and partaking of its backward and forward movement,
but arranged so that its end must move along another bar placed at
an angle with the former. It is this angle which determines the pitch of
the rifling, and by substituting a curved guide-bar for the straight one, an
increasing twist may be obtained in the grooves.
The projectile used with these guns is of a cylindrical form, but pointed
at the head, and the moulds in which these shots are cast are so arranged
that the head of the shot is moulded in iron, while the body is surrounded
with sand. The rapid cooling induced by the contact of the cold metal
causes the head of the shot to solidify very quickly, so that the carbon in
the iron is not separated as in ordinary casting. In consequence of this
treatment, the head of the shot possesses the hardness of steel, and is therefore
well adapted for penetrating iron plates or other structures. The projectiles
are turned in a lathe to the exact size, and then shallow circular
cavities are bored in them, and into these cavities brass studs, which are
simply short cylinders of a diameter slightly larger than the cavities, are
forced by pressure. The projecting studs are then turned so as accurately
to fit the spiral grooves of the guns. Thus the projectile in traversing the
bore of the piece is forced to make a revolution, or part of a revolution,
about its axis, and the rapid rotation thus imparted has the effect of keeping
the axis of the missile always parallel to its original direction. Thus
vastly increased accuracy of firing is obtained.
Fig. 95.—Millwall Shield after being battered with Heavy Shot.—Front View.
Fig. 96.—Rear View of the Millwall Shield.
Shells are also used with the Woolwich rifled guns. The shells are of
the same shape as the solid shots, from which they differ in being cast
hollow, and having their interior filled with gunpowder. Such shells when
used against iron structures require no fuse; they explode in coming into
collision with their object. In other cases, however, the shells are provided
with fuses, which cause the explosion when the shot strikes. Fig. 93, page
195, represents one of the 35–ton guns, made on the plan introduced by
Mr. Fraser. This piece of ordnance is 16 ft. long, 4 ft. 3 in. in diameter at
the breech, and 1 ft. 9 in. at the muzzle. The bore is about 1 ft. Each
200gun can throw a shot or bolt 700 lbs. in weight, with a charge of 120 lbs.
of powder. It is stated that the shot, if fired at a short range, would penetrate
a plate of iron 14 in. thick, and that at a distance of 2,000 yards it
would retain sufficient energy to go through a plate 12 in. thick. The effect
of these ponderous missiles upon thick iron plates is very remarkable.
Targets or shields have been constructed with plates and timber backing,
girders, &c., put together in the strongest possible manner, in order to test
the resisting power of the armour plating and other constructions of our
ironclad ships. The above two cuts, Figs. 95 and 96, are representations
of the appearance of the front and back of a very strong shield of this description,
after having been struck with a few 600 lb. shots fired from the
25–ton gun. The shots with chilled heads, already referred to, sometimes
201were found to penetrate completely through the 8 in. front plate, and the
6 in. of solid teak, and the 6 in. of plating at the back. The shield, though
strongly constructed with massive plates of iron, only served to prove the
relative superiority of the artillery of that day, which was at the time when
our century had yet about thirty years to run. Up to 1876 no confidence
was placed in steel as a resisting material, a circumstance perhaps not
much to be wondered at, as its capabilities had not then been developed
by the newer processes of manufacture, described in our article on Iron;
nor had mechanicians acquired the power of operating with large masses
of the metal. Since then it has come about that only steel is relied upon
for efficiently resisting the penetration of projectiles, iron being held of no
account except as a backing. There has always been a rivalry between
the artillerist and the naval constructor, and this contest between the
attacking and the defending agencies is well illustrated in the table on
page 166, where the parallel advance in the destructive power of guns and
in the resisting power of our war-ships is exhibited in a numerical form.
Fig. 97.—Comparative Sizes of 35 and 81 ton Guns.
A, 35–ton; B, 81–ton.
The 35–ton Fraser guns were at the time of their production humorously
called in the newspapers “Woolwich infants”; but it was not long before
they might in another sense be called infants in comparison with a still
larger gun of 81 tons weight constructed at Woolwich shortly before iron-coiling
and muzzle-loading were set aside. Fig. 97 shows the relative
dimensions of the 35–ton and 81–ton guns: the latter was built up in the
same way as the 9–inch gun described above, but the coils were necessarily
longer and the chase was formed in three parts instead of two.
The total length of this gun was 27 feet, and the bore was about 24 feet
long and 14 in. in diameter, and the weight of the shot about 1000 lbs.,
with sufficient energy to penetrate at a considerable distance an iron
plate 20 in. in thickness. It was for the manufacture of these very large
guns that the great steam hammer, represented in Plate III., was erected
at Woolwich.
The 81–ton gun was the largest muzzle-loader ever made in the
national gun factory at the time when such huge weapons were in
request; but in 1876 its dimensions were surpassed by those of a few
100–ton guns built at Elswick to the order of the Italian Government for
202mounting on their most formidable ironclads. These guns have a calibre
of 17·72 inches, and are provided with a chamber of somewhat larger bore
to receive the charge of powder. They are built up on the Armstrong
shrinkage principle, and comprise as many as twenty different tubes,
jackets, hoops, screws, etc., and are undoubtedly the most powerful
muzzle-loading weapons ever constructed. It happened, just as these
guns were completed, that the British Government, apprehensive at the
time of a war with Russia, exercised its rights of purchasing two of them,
one to be mounted at Gibraltar, the other at Malta.
The Elswick establishment soon afterwards surpassed all its former
achievements in building great guns, by designing and constructing the
huge breech-loaders, one of which forms the subject of our Plate XII.
These are known as the Armstrong 110–ton guns; they are formed of
solid steel throughout, and their weight is accurately 247,795 lbs., or 110
tons 12 cwts. 51 lbs. The total length of the gun is 43 ft. 8 in., and of
this 40 ft. 7 in. is occupied by the bore, along which the rifling extends 33 ft.
1 in. The calibre of the rifled part is 16¼ in., and the diameter of the
powder chamber is somewhat greater. The regulation charge of powder
weighs 960 lbs., although the guns are tested with still greater charges.
The weight of the projectile is 1,800 lbs., and it leaves the muzzle with a
velocity of 2,128 ft. per second, which is equivalent to a dynamical energy
of 56,520 foot-tons. What this means will perhaps be better understood,
not by describing experiments such as those on the Millwall Shield, the
results of which are depicted in Figs. 95 and 96, but by stating that if the
shot from the 110–ton gun encountered a solid wall of wrought iron a yard
thick, it would pass through it. The Elswick 110–ton gun is, in fact, the
most powerful piece of ordnance that has ever been constructed. There
are no trunnions to these great guns, but they are encircled by massive
rings of metal, between which pass strong steel bands that tie the gun to
its carriage, or, rather, to the heavy steel frame on which it is mounted,
and which slides on a couple of girders. The force of the recoil acts on
a hydraulic ram that passes through the lower part of the supporting
frame. The whole working of the gun is done by hydraulic power, and,
indeed, the same method has been applied by the Elswick firm to the
handling of all heavy guns. By hydraulic power, maintained automatically
by a pumping engine exercising a pressure of from 800 lbs. to 1,000
lbs. per square inch, are operated the whole of the movements required
for bringing the cartridge and the projectile from the magazine; for
unscrewing the breech block, withdrawing it, and moving it aside; for
pushing home the shot and the cartridge to their places in the bore; for
closing the breech and screwing up the block; for rotating the turret
within which the gun is mounted, or in other cases for ramming the piece
in or out, and for elevating or depressing it. It is, indeed, obvious that
such ponderous masses of metal as form the barrels and projectiles of
these 110–ton and other guns of the larger sizes could not be handled to
advantage by any of the ordinary mechanical appliances. But by the
application of the hydraulic principle, a very few men are able to work
the largest guns with the greatest ease, for their personal labour is thus
reduced to the mere manipulation of levers. On board ship the power
required for working large guns has lately been sometimes supplied by a
system of shafting driven by a steam engine and provided with drums
and pulleys, exactly as in an engineer’s workshop. Great care has also
been bestowed upon the mounting of the smaller guns, which are so nicely
203poised on their bearings and provided with such accurately fitted racks,
pinions, etc., that a steel gun of 10 ft. in length can easily be pointed in
any direction by the touch of a child’s hand. The mechanical arrangements
are now so admirably adapted for facility of working that, unless
in the rude shocks of actual warfare the nicely adjusted machinery is
found to be liable to be thrown out of gear, these applications of the
engineer’s skill may be considered as having done all that was required
to bring our modern weapons to perfection.
PLATE XII.
THE 110–TON ARMSTRONG GUN.
With the construction of the 110–ton we arrive at a period when commences
a new era in guns—and especially in the armament of war-ships—necessitated
by various circumstances, amongst which may be named
the invention of torpedoes and the building of swiftly moving torpedo-boats,
and of still swifter “torpedo-boat catchers or destroyers”; so that
guns that could be worked only at comparatively long intervals were at
a great disadvantage. Again, about 1880, were published the records of
a most elaborate and important series of researches conducted by Captain
Noble and Sir F. Abel, the chemist of our War Department. They had
investigated all the conditions attending the combustion of gunpowder
in confined spaces, the nature and quantities of the products, the temperature
and pressures of the confined gases, etc. The information thus
afforded was extremely valuable; but besides this, direct experiments
made with actual guns were carried out, more particularly at Elswick,
in which the speed of the projectiles at every few inches of their travel
along the bore of the piece was ascertained, and also the pressures of the
powder gases at any point. The way in which this is done we shall
explain on another page. (See article on Recording Instruments.)
So long as muzzle-loading was in use, guns were necessarily made
short, for had they not to be run in from the port-holes and embrasures
of forts in order to be loaded? Now there was an obvious disadvantage
in this, for the projectile left the gun before the expansive force of
the gases had been spent that could have imparted additional velocity.
When however muzzle-loading was abandoned, and especially when strong
and trustworthy steel became available for the construction of the gun
throughout, there was no reason to waste in this way the power of the
charge, so that barrels were made lighter, much longer in proportion to
the calibre, and every part accurately adapted in strength to the strain
to be resisted. For instances of increasing length, take the 38–ton 12–inch
guns built up at Woolwich (of only seven pieces) for H.M.S. Thunderer
(see Fig. 93), on Mr. Fraser’s plan. These had a bore equal to only 16
times their calibre, while in the Armstrong 100–ton guns the bore is 21
calibres long; and in the 110–ton guns the total length of the chase is
31 times the diameter of the rifled part. It has since been the practice
to make the bore of guns from 30 to 40 calibres in length.
The effect of a longer chase used with an appropriate charge is very
clearly and instructively shown by the diagram Fig. 98, which is by
permission copied from the very comprehensive work by Messrs. E. W.
Lloyd and A. G. Hadcock, entitled Artillery: its Progress and Present
Position. The reader should not pass over this diagram until he has
thoroughly understood it, for it is an excellent example of the graphic
method of presenting the results of scientific investigations. At the
lower part of the diagram there are drawn to scale half-sections of a long
and of a short gun. The horizontal line above is marked in equal parts
representing feet numbered from the base of the projectiles. The upright
204line on the left numbered at every fourth division is the scale for the
pressures in tons per square inch on the base of the projectile, and these
are represented by the height of the plain curves above the horizontal
line at each point in the travel of the shot. The dotted lines represent
in the same way, but not on the same scale as the former, the velocity
with which the base of the projectile passes every point in the chase.
The figures 2, 4, and 6 on the upright line at the right-hand side refer
only to pressures: the velocities scale is such that the point where the
dotted meets the right-hand one is 2,680 units above the horizontal
line, as the middle upright in the same way is 1,561 high, and the heights
of the dotted lines represent each on the same scale the velocities of the
bases of the projectiles at the corresponding parts of the chases. The
shorter gun has the rifled part of the chase 15·4 calibres long; the corresponding
part of the longer is nearly 33 calibres. The short 7–inch gun
has a charge of 30 lbs. of gunpowder, and its projectile weighed 115 lbs.
The longer 6–inch gun was not charged with gunpowder, but with the
more powerful modern explosive cordite (see Index), of which there was
19·5 lbs., and its projectile weighed 100 lbs. The charges were so
adjusted that the shots had the same initial maximum pressure of 20 tons
per square inch applied to them. Now the cordite, though much more
powerful than gunpowder (that is, a given weight will produce far more
gas), is slower in its ignition, continuing longer to supply gas. The
maximum pressure, 20 tons in both cases, is suddenly attained by the
gunpowder gases, when the shot has hardly moved 6 inches onward, and
the pressure declines rapidly as the moving shot leaves more space for
the gas; while the cordite gases produce their greatest pressure more
gradually at a part where the shot is already about 20 inches on its way,
and not only do their highest pressures continue for a greater distance,—but
the decline is far less rapid than in the other case. It will be observed
by the intersection of the dotted lines, that when the shots in each case
have moved about 2 ft. their velocities are equal. They finally leave the
muzzles with the velocities marked on the diagram, and if the reader will
apply the formula given on page 174 he will obtain their respective energies
in foot-lbs.; but for large amounts like these it is more usual to state the
energy in foot-tons, which of course will be arrived at by dividing the
foot-lbs. numbers by 2,240, and these will work out in the one case to
4978·9 ft.-tons, and in the other to 1942·5 ft.-tons. The shot from the long
gun will therefore have more than 2½ times the destructive power of the
other.
Fig. 98.—Diagram of Velocities and Pressure.
The operations required in constructing guns are multiform, and have
to be very carefully conducted so that the workmanship shall be of the
best quality. The finest ores are selected for reduction, and the steel is
obtained by the Siemens-Martin process already described. It must be
free from sulphur and phosphorus, and contain such proportions of carbon,
silicon, and manganese as experience has shown to be best, and its composition
is ascertained by careful chemical analysis before it is used.
The fluid steel is run into large ladles lined with fire-brick, and provided
with an opening in the bottom from which the metal can be allowed to
run out into the ingot moulds, the size and proportions of these being in
accordance with the object required; some admitting of as much as
80 tons at one operation. When a barrel or hoop is required of not less
than 6 inches internal diameter the ingot is cut to the required length
and roughly bored. The ingot is then heated, a long cylindrical steel bar
206is put through the hole, and under a hydraulic press the hot metal is
squeezed into greater length and less diameter. The hole first bored
through the ingot is of somewhat greater, and the steel bar (called a
mandril) of less, diameter than required in the finished piece. Portions
are cut from each end of what is now called the forging and subjected to
mechanical tests: if these are satisfactory, the forging is rough bored and
turned on the outside. It is then annealed, by being heated and allowed
to cool very slowly. The next operation is to harden the metal by raising
it to a certain temperature, at which it is immersed in rape oil until cold.
Then the piece is again annealed, and fine-turned and bored. All these
operations have to be performed not only on the barrel, but also on each
hoop, before the hoops are shrunk on, and the greatest nicety of measurement
is required in each piece. Then the gun has to be turned on the
outside, the screw for the breech piece cut, the bore rifled, etc. The
object of the annealing is to relieve the metal from internal strains. It
will not be wondered at that months are required for the construction of
the larger kind of guns. Thus at Elswick a 6 in. quick firing gun, upon
which men are employed night and day, cannot be completed in less
than five months, and sixteen months are required for making a 67–ton
gun.
We may take as an illustration of the progress of modern artillery one
of the products of the Elswick factory which has just been referred to,
and for which the demand from all quarters has been unprecedentedly
great, namely, the 4·7 inch gun. This weapon is mounted in various
manners according to the position it has to occupy, whether for a land
defence, or on ship-board between decks, or on the upper deck. The
arrangement shown in Fig. 99, which is reproduced from Messrs. Lloyd
& Hadcock’s work, is known as the centre pivot mounting, and is
suitable for such a position as the upper deck of a ship. The reader
should compare the proportions and mounting of this weapon with those
of the old 32–pounder sketched in Fig. 90, observing the very much greater
comparative length of the modern weapon, and the mechanism for elevating
and training it (which, however, the scale of the drawing crowds into
too small a space to show as it deserves). C is a projection from the
breech, to which is attached the piston of the recoil press; at T is the
handle for training, which actuates a worm at V; the elevation is regulated
by the turning of the four-armed wheel. The long chase of the
gun projects in front; but the mounting and the breech machinery are
protected by shields of thick steel, of which the sections of two plates are
denoted by the dark upright parts in front. These are fixed; but a
movable plate above the gun can be raised or lowered into an inclined
position, for better taking sights. In the figure this is shown as open
and in a horizontal position. This gun is provided with sights by which
it can be aimed at night; that is, the sights can be illuminated by small
electric lamps suitably placed; the wires connecting these with voltaic
battery cells carried on the mounting are indicated. The figure represents
the gun as constructed about 1893, but the improvements that
are continually being made have brought about some modifications in
the details.
Fig. 99.—Elswick 4·7 inch Q. F. Gun on Pivot Mounting.
Very notable among the productions of the great Elswick factory are
the quick firing guns. These were at first confined to guns of small
calibre, such as the 6–pounders. They are, of course, all breech-loaders,
and the powder and shot are both contained in a single metallic cartridge
208case. A more formidable weapon of the same class is the 45–pounder
rapid firing gun, which, like the rest, is constructed entirely of steel, with
a total length of 16 ft. 2½ in., a calibre of 4·724 in., and a length of bore
equal to 40 diameters. The weight of this gun is 41 cwt., and it throws
a shell of 45 lbs. weight with a 12–lb. charge of gunpowder. Quick firing
guns having a calibre of 6 in. are now also made in great numbers for arming
our ironclads. The breech block in the quick firing guns turns aside
on a hinge, and after the introduction of the cartridge it is closed and
screwed up to its place by a slight turn of a handle. The piece is then
pointed and trained by aid of mechanical gearing as in the case of the
heavier guns. But Mr. Hotchkiss has introduced a simpler method of
elevating and training his 3–pounder and 6–pounder quick firing guns, by
attaching to the rear, and unaffected by the recoil, a shoulder piece
against which the marksman can lean, and move the weapon as he takes
his aim. Though these guns weigh respectively 4½ cwt. and 7 cwt., they
can thus be pointed with the greatest ease. The firing is done by pulling
a trigger in what seems like the stock of a pistol. The empty cartridge
case is automatically extracted from the firing chamber by the act of
opening the breech, and it drops to the ground. Ten or twelve rounds
per minute can be fired from these guns, and Lord Armstrong has advocated
the use of a number of them for naval armament in preference to
that of a few ordinary breech-loaders of more unwieldy dimensions. He
has calculated that in a given time a far greater weight of metal can be
projected from a vessel armed with quick firing guns than from one provided
only with the heavier class of cannons.
The breech pieces in the Elswick guns are closed on the “interrupted
screw” system—that is, a very large screw thread of V-shaped section is
cut in the barrel at the breech end, and a corresponding thread on the
principal part of the breech block, which is, of course, capable of rotating
about the axis. The screw threads, however, are not continuous, segments
parallel to the axis being cut away, the spaces in the outer thread
corresponding with the projecting parts in the inner, and vice versâ, so
that when the block is pushed home, one very small part of a turn
suffices to engage all the threads. The screw is also made conical, and
is so cut into steps, as it were, that great resisting power is brought into
play. The Elswick guns are provided with hydraulic buffers for checking
the recoil, and the principle is applied in various modified forms. In
some cases the pistons allow for the water a passage, which towards
the end gradually diminishes. This is the arrangement for the 3–pounder
rapid firing Hotchkiss gun, and the force of the recoil is made at the same
time to compress two springs, which serve to return the gun to the firing
position. This very handy gun is said to be able to fire twenty rounds
per minute. In Mr. Vavasseur’s plan of mounting, the recoil is checked
by ports, or openings, in the piston of a hydraulic cylinder being gradually
closed, which is easily arranged by making a spiral groove within
the cylinder, which gives a small axial motion to part of the piston.
Fig. 100.—The Moncrieff Gun raised and ready for firing.
Fig. 101.—Moncrieff Gun lowered for loading.
An extremely effective plan for the defence of coasts and harbours was
originated by Colonel Moncrieff, when about 1863 he contrived a method
of mounting large guns on the disappearing system, by which almost
complete protection against hostile fire is given to both gun and gunners.
He utilizes the recoil as a means of bringing the gun down into a protected
position the moment it has been fired, and retains this energy by
a simple arrangement until the piece has been reloaded, when it is
209allowed to expend itself by again raising the gun above the parapet into
the original firing position. The configuration and action of Colonel
Moncrieff’s gun-carriage will be understood by an inspection of the
annexed illustrations, where in Fig. 100 is shown the gun raised above
210the parapet and ready for firing. When the discharge takes place, the
gun, if free, would move backwards with a certain speed, but the disposition
of the mounting is such that this initial velocity receives no sudden
check, the force being expended in raising a heavy counterpoise, and at
the same time the gun is permitted to descend, while maintaining a direction
parallel to its firing position. At the end of the descent, which, it
must be understood, is caused by the force of the recoil, and not by the
counterpoise, for this more than balances the weight of the gun, the
latter is retained as shown in Fig. 101 until it has been reloaded; and
when it has again to be fired, it is released so as to allow the descent of
the counterpoise to raise it once more into position. The great advantage
of this invention is the protection afforded to the artillerymen and
gun while loading; and even the aiming can be accomplished by mirrors,
so that the men are exposed to no danger, except from “vertical fire,”
which involves but little risk.
Colonel Moncrieff took out a patent for his invention in 1864, but committed
the practical working out of his idea to the firm of Sir W. G.
Armstrong & Co., in whose hands the design was ultimately transformed
from the original somewhat cumbersome arrangement of the mounting
into the compact and manageable form shown in Fig. 102, which represents
a 13·9 inch 68–ton breech-loading disappearing gun on the Elswick
hydro-pneumatic mounting. The principle of hydraulic power is fully
explained in our article on that subject, and an example of its application
to cranes as devised by Sir W. Armstrong is there described. When
guns began to be made very large, and projectiles weighing several cwts.
had to be dealt with, the application of power in some form became
essential for loading, running out, elevating, training, etc.; and though
steam-power naturally was first used, hydraulic power was adopted at
Elswick, and has been there applied to the mountings of large guns with
the greatest success by Mr. G. W. Rendel. To mention the various
arrangements in which this power is applied, or to attempt any description
of the elaborate machinery by which it is regulated, would carry us
far beyond our limits. But the powerful weapon depicted in Fig. 102 is
designed to be worked only by the manual effort of a few men. In this
mounting the pressure of condensed air sustains the gun in the firing
position; that pressure, acting upon the water in the recoil presses, having
previously forced up their rams so as to turn into a nearly vertical position
the strong brackets or beams on which the trunnions are supported.
The recoil is checked in the usual way by the forcing of the water through
small ports or valves as the ram descends, but these valves are so
arranged that the water is in part forced back into the air chamber, and
there recompresses the air, to restore the power for again raising the gun.
The pressure in the air chamber when the gun is down may be about
1,400 lbs. per square inch; when it is up this will be reduced to perhaps
one half by the expansion of the air in doing work. We have here the
reaction of compressed air taking the place of the gravity of the counterpoise
originally designed. There are in this hydro-pneumatic mounting
a number of adjusting appliances, such as forcing pumps, brakes, etc.,
for regulating the pressures, or quantity of liquid, as, for instance, when
lowering the gun without any recoil action in operation. Then again,
with any change in the weight of projectile or in the powder charge,
there would be a corresponding change in the power of the recoil, and
therefore the necessity for compensatory adjustments, which are made
212with great readiness. The nicety with which the parts are adapted to
each other in this mounting must be obvious, when we observe the
magnitude of the mass to be moved with the least delay, and brought to
rest, quite gently and exactly, in a new position. Details cannot here be
given even of the method by which the valves in the recoil cylinders are
automatically controlled for this purpose. Means are also supplied for
setting the gun, while still in its protected position, to the required angle
of elevation or depression. The adjustment is made by the long rods
attached near the breech and set at their lower ends to the position giving
the intended angle to the raised gun. The varied and powerful strains
to which the parts of this mechanism are subject, and which have had to
be calculated and provided for, may be inferred from the enormous
recoil energy of the gun, which under ordinary conditions amounts to no
less than 730 foot-tons. The gun is provided with ordinary, and also
with reflecting, sights, so that no one need be exposed to the enemy’s
fire. Protective armour above the gun is not required, as the pit itself
being usually on some elevation is imperceptible to the enemy, and the
gun is visible but for a few seconds, forming a quite inconspicuous object.
The pit in which the gun is mounted is commonly lined with concrete.
Italy, England, Norway, Japan and other countries have appreciated the
advantages of the disappearing system in providing the most powerful
coast defences yet devised, and a great many guns have been mounted
on this principle.
Fig. 102.—68–ton Gun on Elswick Hydro-Pneumatic Mounting.
An extraordinary piece of ordnance is represented in Fig. 103. It is
one of two huge mortars, the idea of which presented itself to Mr. Mallet
during the Crimean War, the intention being to throw into the Russian
lines spherical shells a yard in diameter, which would, in fact, have constituted
powerful mines, rendering it impossible for the fortifications to
continue tenable. Mallet’s original design was to project these shells
from mortars of no less than 40 tons weight. When it was pointed out
that the transport of so heavy a mass would be impracticable, the design
was changed to admit of the mortar being made in pieces not exceeding
eleven tons in weight, and built up where required. During the most
active period in the siege of Sebastopol this plan was submitted to Lord
Palmerston, who at once ordered two of these apparently formidable
pieces to be constructed, without waiting for official examinations of the
scheme, and the usual reports of experts,—promptness in this case being
considered of the utmost importance. A contract was made with a
private firm, who undertook to deliver them in ten weeks. But the
difficulties attending such constructions not being understood at the
time, delays arose, the contractors failed, and two years elapsed before
the mortars were completed. In the meantime peace had been concluded,
and the mortars were never fired against any hostile works; but experiments
were made with one of them at Woolwich. The heaviest of the
shells it was intended to project weighed 2,940 lbs., and for this it was
proposed to use a charge of 80 lbs. of gunpowder. In the experiments
the charges first used were low, but gradually increased: when it was
found that after every few rounds repairs became necessary in consequence
of the weak points in the construction, and after the nineteenth round
the mortar was so much damaged that the trials were definitely discontinued.
The other mortar, though mounted, was never fired, but remains
at Woolwich, an object of some interest to artillerists, especially since
there has been some talk of reverting to this very old-fashioned form of
213ordnance as a means of attacking ironclads in their most vulnerable
direction by the so-called vertical fire. In one of the rounds of the
Mallet mortar tried at Woolwich, a shell weighing 2,400 lbs. was thrown
by a charge of 70 lbs. of gunpowder a distance of more than a mile and
a half, and it buried itself in the soil to a very great depth.
Fig. 103.—Mallet’s Mortar
For high-elevation firing, howitzers will more probably be the form of
ordnance most in use. The range of the howitzer is determined by the
angle at which it is elevated, whereas with the mortar it is chiefly by
variation of the powder charge that the aim is adjusted. Many of the
old short 9 in. muzzle-loaders have already been converted into 11 in.
214rifled howitzers, and these are likely to prove of great service in defending
our harbours and channels against war vessels.
Some account has been given in a preceding article of the great steel
works of Krupp & Co. at Essen, and the place has been noted as one of
the greatest gun factories in the world during the second half of our
century. The process there practised of casting crucible steel ingots, and
already described, is precisely that used in the first stage of gun-making.
The steel for guns put into the crucibles is a carefully adjusted mixture
of one quality of iron puddled into steel and subjected to certain treatment;
the other portion is made from a different quality of iron from
which all the carbon has been puddled out. The cast ingot is forged
under a great steam hammer, bored, turned, and steel hoops shrunk upon
it, in several layers, and other operations are performed upon it like
those which have already been mentioned. A 14 in. gun is said to require
sixteen months for its manufacture, and its cost to be about £20,000.
Fig. 104.—32–pounder Krupp Siege Gun, with Breech-piece open.
Artillerists had long carried on a warm controversy as to the relative
merits of wrought iron and steel in gun construction, the latter material
being regarded with shyness on account of its want of uniformity as
formerly produced. Krupp however began as early as 1847 to make guns
of his excellent crucible steel, and through bad report and good report
confined himself to this material until, it is asserted, by 1878 he had
supplied over 17,000 steel guns of all calibres. He began by making a
3–pounder gun, but soon produced pieces of larger size, all of which were
bored and turned out of solid masses of metal. At a later period the
plan of shrinking on strengthening hoops of steel was adopted. The Krupp
guns have found extensive favour, and many very heavy ones have been
made, some indeed of greater weight than the 110–ton Armstrong; but
the excess of weight is due to the mass of metal which the Krupp construction
of the breech mechanism requires. Thus Krupp’s 120–ton gun
has a muzzle energy of but 45,796 foot-tons, while that of the Elswick
piece is 55,105 foot-tons.
Fig. 105.—The Citadel of Strasburg after the Prussian Bombardment.
The breech arrangement in the Krupp guns consists of a lateral slot
into which slides a closing block after the charge has been inserted from
the rear. An obsolete form of this breech piece is seen in Fig. 104, which
215represents a 32–pounder gun such as was used in sieges by the Prussians
in the Franco-German War. It will be observed here that the slot and
breech piece are of rectangular form; but this shape, causing the piece
to be weak where most strength was required, was afterwards altered into
a D-shaped section, the curved side being of course to the rear. That
difficulty which baffled the earliest attempts at breech-loading is the
same that has given much trouble to modern gunmakers. It consists in
so closing the breech that no escape of the powder gases can take place
there at the moment of discharge. When we remember that the
momentary pressure of the gases in the powder chamber may amount
to more than 40 tons on the square inch, we can well understand the
enormous velocity with which they will rush forth from even the smallest
interspace between the base of the gun and the breech block, but we can
hardly realise without actual inspection the mechanical action they produce
in their passage: when once the escape occurs, a channel is cut in
the metal as if part had been removed by an instrument, and the piece in
that condition is disabled for further use. Several devices are in use
obtaining perfect closure of the breech, which is technically called obturation
(Latin, obturare, to close up). One of these consists in fitting closely
into the circumference of the bore a ring of very elastic steel, turned up
at the edges towards the powder chamber. The gas pressure forces the
edge of this ring still more closely against the interior of the powder
chamber, much in the same way as the Bramah collar acts in the hydraulic
press (see Fig. 165). The shaded circle shown on the breech piece in
Fig. 104 is an additional device for obtaining obturation. The Broadwell
216ring, as the above-mentioned contrivance is called, is not used in English
guns, but another plan of obtaining a gas-joint has been much adopted,
in which a squeezable pad is by compression forced outwards to close up
the bore.
A very long range was claimed for Krupp’s guns at the time of the
Franco-German War, for at the siege of Paris (1870) it was said they
could hurl projectiles to the distance of five miles, though probably there
was some exaggeration in this statement. There is no doubt however
that the Prussians had very effective and powerful artillery, as may be
gathered from Fig. 105, which is taken from a photograph of part of the
fortifications of Strasburg after the bombardment of that fortress. The
explosive shells used by the Prussians against masses of troops were not
precisely segment shells of the form already described, but the principle
and effect were the same, for the interior was built up of circular rings,
which broke into many pieces when the shell exploded.
Out of the very numerous forms in which modern ordnance is constructed,
we have been able to select but a few examples for illustration
and description. These will suffice, it is hoped, to give an idea of the
progress that the century has witnessed. It would be beyond our scope
to give details of the ingenious mechanical devices that have come to be
applied to guns: such as the breech-closing arrangements, the various
ways in which recoil is controlled and utilized, etc. A good illustration,
had space permitted, of the scientific skill applied to ordnance would be
found in the contrivances fitted to certain projectiles in order to determine
their explosion at the proper moment. These are very different
from the cap or time fuse that did duty in the first half of the century.
We have indeed said little of the projectiles themselves beyond mention
of the Palliser chilled shot and the obsolete studded projectiles. We
have not explained how bands of copper, or other soft metal, are put
round a certain part of the shot or shell, in order that, being forced into
the grooves, the axial rotation may be imparted, or how windage is prevented
by “gas checks” attached to the base of the projectiles. We
must now be contented to conclude this section by showing the structure
of two kinds of explosive shells which have been much used.
Shrapnel shell takes its name from Lieutenant Shrapnel, who was its
inventor about the end of last century, but the projectile began to be used
only in 1808. Fig. 105a is a section showing the shell as a case containing
a number of spherical bullets, of which in the larger shells there are very
many, the interspaces being filled with rosin, poured in when melted; the
bullets are thus prevented from moving about. The figure shows the shell
without the fuse or percussion apparatus, which screws into the hollow
at the front. The bursting charge of gunpowder is behind the bullets,
and when it explodes they travel forward with a greater velocity than
the shell, but with trajectories more or less radiating, carrying with them
wide-spreading destruction and death.
A shrapnel shell may be said to be a short cannon containing its charge
of powder in a thick chamber at the breech end; the sides of the fore
part of the shell are thinner than those of the chamber, and may be said
to form the barrel of the cannon. This cannon is loaded up to the muzzle
with round balls, which vary with the shell in size. An iron disc between
the powder and the bullets represents the wad used in ordinary fowling-pieces.
A false conical head is attached to the shell, so that its outward
appearance is very similar to that of an ordinary cylindro-conoidal shell:
217that is to say, it looks like a very large long Enfield bullet. The spinning
motion which had been communicated to the shell by the rifling of the
gun from which it had been fired causes the barrel filled with bullets to
point in the direction of the object at which the gun has been aimed.
Consequently, when the shrapnel shell is burst, or rather fired off, the
bullets which it contained are streamed forward with actually greater
velocity than that at which the shell had been moving; and the effect
produced is similar to firing grape and canister from a smooth-bore
cannon at a short range.
Fig. 105a.—The Shrapnel and Segment Shells.
Segment shells were first brought into use by Lord Armstrong in 1858
in connection with his breech-loading guns. The segment shell consists
of a thin casing like a huge conical-headed thimble, with a false bottom
attached to it. It is filled with small pieces of iron called “segments,”
cast into shapes which enable them to be built up inside the outer casing
into two or more concentric circular walls. The internal surface of the
inmost wall forms the cavity of the compound or segment shell, and contains
the bursting charge. The segment shell is fitted with a percussion
fuse, which causes it to explode when it strikes. In the shrapnel shell,
the powder charge is situated in rear of the bullets, and consequently
produces the chief effect in a forward direction. In the segment shell,
the powder is contained inside the segments, and therefore produces the
chief effect in a lateral direction. When the shrapnel shell is burst at
the right moment, its effect is greatly superior to that of the segment
shell; on the other hand, the segment shell, when employed at unknown
or varying distances, is far more unlikely to explode at the proper time.
Shrapnel and segment shells can be used with field artillery, i.e.,
2189–pounders, 12–pounders, 16–pounders; and also with heavy rifled guns in
fortresses, viz., 40–pounders, 64–pounders, 7–in. and 9–in. guns. But the
conditions of their service are very different in each case. With regard to
field artillery, the distance of the enemy is rarely known, and is constantly
changing, and hence the men who have to adjust the fuses
would probably be exposed to the fire of the enemy’s artillery, and, consequently,
could not be expected to prepare the fuses with the great care
and nicety which are absolutely necessary to give due effect to the shells.
There are, however, some occasions when the above objections would
not hold good—as, for instance, when field artillery occupy a position in
which they wait the attack of an enemy advancing over ground in which
the distances are known.
Segment shells require no adjustment of their percussion fuse. They
enable the artillerymen to hit off the proper range very quickly, since the
smoke of the shell which bursts on striking tells them at once whether
they are aiming too high or too low.
With regard, however, to the service of heavy rifled guns in fortresses,
the conditions are quite different. In the first place, the distance of all
objects in sight would be well known beforehand; and in the second
place, the fuses of the shells would be carefully cut to the required length
in the bomb-proofs, where the men would be completely sheltered. The
7–in. shrapnel contains 227 bullets, and a 9–in. shrapnel would contain
500 bullets of the same size, and these shells could be burst with extraordinary
accuracy upon objects 5,000, 6,000, or 7,000 yards off.
The name of machine guns has been applied to arms which may be
regarded as in some respects intermediate between cannons and
rifles, since in certain particulars they partake of the nature of both.
Like the former, they are fired from a stand or carriage, and in some of
their forms require more than one man for their working: in the calibre
of their barrels and the weight of their projectiles, they are assimilated
to the rifle, but they are capable of pouring forth their missiles in a very
rapid succession—so rapid indeed as practically to constitute volley
firing. The firing mechanism of the machine gun has always an automatic
character, but the rifle has acquired this feature, so that it cannot
be made a distinguishing mark: on the other hand, since machine guns
have been made to discharge projectiles of such weights as 1 lb. or 3 lb.
there is nothing to separate them from quick-firing ordnance unless it be
the automatic firing.
The idea of combining a number of musket-barrels into one weapon,
so that these barrels may be discharged simultaneously or in rapid succession,
is not new. Attempts were made two hundred years ago to
construct such weapons; but they failed, from the want of good mechanical
adjustments of their parts. Nor would the machine gun have become
the effective weapon it is, but for the timely invention of the rigid metallic-cased
cartridge. Several forms of machine guns have in turn attracted
much attention. There is the Mitrailleur (or Mitrailleuse), of which so
much was heard at the commencement of the Franco-German War,
and of whose deadly powers the French managed to circulate terrible
and mysterious reports, while the weapon itself was kept concealed.
219Whether this arose from the great expectations really entertained of the
destructive effects of the mitrailleur, or whether the reports were circulated
merely to inspire the French troops with confidence, would be difficult
to determine. Our own policy in regard to new implements of war is
not to attempt to conceal their construction. Experience has shown that
no secret of the least value can long be preserved within the walls of an
arsenal, although the French certainly apparently succeeded in surrounding
their invention with mystery for a while. The machine gun, or
“battery,” invented by Mr. Gatling, an American, is said by English
artillerists to be free from many defects of the French mitrailleur. In
1870 a committee of English military men was appointed to examine the
powers of several forms of mitrailleur, with a view to reporting upon the
advisability or otherwise of introducing this arm into the British service.
They recommended for certain purposes the Gatling battery gun.
Fig. 105b.—The Gatling Gun.—Rear View.
In the Gatling the barrels, ten in number, are distinct and separate, being
screwed into a solid revolving piece towards the breech end, and passing
near their muzzles through a plate, by which they are kept parallel to each
other. The whole revolves with a shaft, turning in bearings placed front
and rear in an oblong fixed frame, and carrying two other pieces, which
rotate with it. These are the “carrier” and the lock cylinder. Fig. 105b
gives a rear view, and Fig. 105c a side view, of the Gatling battery gun.
The weapon is made of three sizes, the largest one firing bullets 1 in. in
diameter, weighing ½ lb., the smallest discharging bullets of ·45 in.
diameter. The small Gatling is said to be effective at a range of more
than a mile and a quarter, and can discharge 400 bullets or more in one
minute. Mr. Gatling thus describes his invention:
“The gun consists of a series of barrels in combination with a grooved
220carrier and lock cylinder. All these several parts are rigidly secured upon
a main shaft. There are as many grooves in the carrier, and as many
holes in the lock cylinder, as there are barrels. Each barrel is furnished
with one lock, so that a gun with ten barrels has ten locks. The locks
work in the holes formed in the lock cylinder on a line with the axis of the
barrels. The lock cylinder, which contains the lock, is surrounded by a
casing, which is fastened to a frame, to which trimmers are attached.
There is a partition in the casing, through which there is an opening, and
into which the main shaft, which carries the lock cylinder, carrier, and
barrels, is journaled. The main shaft is also at its front end journaled in
the front part of the frame. In front of the partition in the casing is placed
a cam, provided with spiral surfaces or inclined planes.
“This cam is rigidly fastened to the casing, and is used to impart a
reciprocating motion to the locks when the gun is rotated. There is also
in the front part of the casing a cocking ring which surrounds the lock
cylinder, is attached to the casing, and has on its rear surface an inclined
plane with an abrupt shoulder. This ring and its projection are used for
cocking and firing the gun. This ring, the spiral cam, and the locks make
up the loading and firing mechanism.
“On the rear end of the main shaft, in rear of the partition in the casing,
is located a gear-wheel, which works to a pinion on the crank-shaft. The
rear of the casing is closed by the cascable plate. There is hinged to the
frame in front of the breech-casing a curved plate, covering partially the
grooved carrier, into which is formed a hopper or opening, through which
the cartridges are fed to the gun from feed-cases. The frame which supports
the gun is mounted upon the carriage used for the transportation of
the gun.
“The operation of the gun is very simple. One man places a feed-case
filled with cartridges into the hopper; another man turns the crank, which,
by the agency of the gearing, revolves the main shaft, carrying with it the
lock cylinder, carrier, barrels, and locks. As the gun is rotated, the cartridges,
one by one, drop into the grooves of the carrier from the feed-cases,
and instantly the lock, by its impingement on the spiral cam surfaces,
moves forward to load the cartridge, and when the butt-end of the lock
gets on the highest projection of the cam, the charge is fired, through the
agency of the cocking device, which at this point liberates the lock, spring,
and hammer, and explodes the cartridge. As soon as the charge is fired,
the lock, as the gun is revolved, is drawn back by the agency of the spiral
surface in the cam acting on a lug of the lock, bringing with it the shell of
the cartridge after it has been fired, which is dropped on the ground. Thus,
it will be seen, when the gun is rotated, the locks in rapid succession move
forward to load and fire, and return to extract the cartridge-shells. In other
words, the whole operation of loading, closing the breech, discharging, and
expelling the empty cartridge-shells is conducted while the barrels are
kept in continuous revolving movement. It must be borne in mind that
while the locks revolve with the barrels, they have also, in their line of
travel, a spiral reciprocating movement; that is, each lock revolves once
and moves forward and back at each revolution of the gun.
“The gun is so novel in its construction and operation that it is almost
impossible to describe it minutely without the aid of drawings. Its main
features may be summed up thus: 1st.—Each barrel in the gun is provided
with its own independent lock or firing mechanism. 2nd.—All the locks
revolve simultaneously with the barrels, carrier, and inner breech, when the
221gun is in operation. The locks also have, as stated, a reciprocating motion
when the gun is rotated. The gun cannot be fired when either the barrels
or locks are at rest.”
There is a beautiful mechanical principle developed in the gun, viz., that
while the gun itself is under uniform constant rotary motion, the locks
rotate with the barrels and breech, and at the same time have a longitudinal
reciprocating motion, performing the consecutive operations of
loading, cocking, and firing without any pause whatever in the several and
continuous operations.
The small Gatling is supplied with another improvement called the
“drum feed.” This case is divided into sixteen sections, each of which
contains twenty-five cartridges, and is placed on a vertical axis on the top
of the gun. As fast as one section is discharged, it rotates, and brings
another section over the feed aperture, until the whole 400 charges are
expended.
Fig. 105c.—The Gatling Gun.—Front View.
After a careful comparison of the effects of field artillery firing shrapnel,
the committee concluded that the Gatling would be more destructive in
the open at distances up to 1,200 yards, but that it is not comparable to
artillery in effect at greater distances, or where the ground is covered by
trees, brushwood, earthworks, &c. The mitrailleur, however, would soon be
knocked over by artillery if exposed, and therefore will probably only be
employed in situations under shelter from such fire. An English officer,
who witnessed the effects of mitrailleur fire at the battle of Beaugency,
looks upon the mitrailleur as representing a certain number of infantry,
for whom there is not room on the ground, suddenly placed forward at the
proper moment at a decisive point to bring a crushing fire upon the enemy.
Many other eye-witnesses have spoken of the fearfully deadly effect of the
mitrailleur in certain actions during the Franco-German War.
Mr. Gatling contends that, shot for shot, his machine is more accurate
than infantry, and certainly the absence of nerves will ensure steadiness;
222while so few men (four) are necessary to work the gun that the exposure of
life is less. No re-sighting and re-laying are necessary between each discharge.
When the gun is once sighted its carriage does not move, except
at the will of the operator; and the gun can be moved laterally when firing
is going on, so as to sweep the section of a circle of 12° or more without
moving the trail or changing the wheels of the carriage. The smoke of
battle, therefore, does not interfere with its precision.
Whatever may be the part this new weapon is destined to play in the
wars of the future, we know that every European Power has now provided
itself with some machine guns. The Germans have those they took from
the French, who adhere to their old pattern. The Russians have made
numbers of Gatlings, each of which can send out, it is said, 1,000 shots per
minute, and improvements have been effected, so as to obtain a lateral
sweep for the fire.
Fig. 105d.—The Montigny Mitrailleur.
A competitor to the Gatling presents itself in the Belgian mitrailleur, the
Montigny, Fig. 105d. This gun, like the Gatling, is made of several different
sizes, the smallest containing nineteen barrels and the largest thirty-seven.
The barrels are all fitted into a wrought iron tube, which thus constitutes
the compound barrel of the weapon. At the breech end of this
barrel is the movable portion and the mechanism by which it is worked.
The movable portion consists mainly of a short metallic cylinder of about
the same diameter as the compound barrel, and this is pierced with a
number of holes which correspond exactly with the position of the gun-barrels,
of which they would form so many prolongations. In each of the
holes or tubes a steel piston works freely; and when its front end is made
even with the front surface of the short cylinder, a spiral spring, which is
also contained in each of the tubes, is compressed. The short cylinder
moves as a whole backwards and forwards in the direction of the axis of
the piece, the movement being given by a lever to the shorter arm of which
the movable piece is attached. When the gun is to be loaded this piece is
drawn backwards by raising the lever, when the spiral springs are relieved
223from compression, and the heads of the pistons press lightly against a flat
steel plate in front of them. The withdrawal of the breech-block gives space
for a steel plate, bored with holes corresponding to the barrels, to be slid
down vertically; and this plate holds in each hole a cartridge, the head of
each cartridge being, when the plate has dropped into its position, exactly
opposite to the barrel, into which it is thrust, when the movable breech-block
is made to advance. The anterior face of this breech-block is formed
of a plate containing a number of holes again corresponding to the barrels,
and in each hole is a little short rod of metal, which has in front a projecting
point that can be made to protrude through a small aperture in the
front of the plate, the said small apertures exactly agreeing in position with
the centres of the barrels, and being the only perforations in the front of
the plate. The back of the plate has also openings through which the
heads of the pistons can pass, and by hitting the little pieces, or strikers,
cause their points to pass out through the apertures in front of the plate,
and enter the base of the cartridges, where fulminate is placed. The plate
filled with cartridges has a bevelled edge, and the points of the strikers are
pushed back by it as it descends. The heads of the pistons are separated
until the moment of discharge from the recesses containing the strikers by
the flat steel plate or shutter already mentioned. The effect, therefore, of
pushing the breech-block forward is to ram the cartridges into the barrels,
and at the same time the spiral springs are compressed, and the heads of
the pistons press against the steel shutter which separates them from the
strikers, so that the whole of the breech mechanism is thus closed up.
When the piece is to be fired a handle is turned, which draws down the
steel shutter and permits the pistons to leap forward one by one, and hit
the strikers, so that the points of the latter enter the cartridges and inflame
the fulminate. The shutter is cut at its upper edge into steps, so that no
two adjoining barrels are fired at once. The whole of the thirty-seven
barrels can be fired by one and a quarter turns of the handle, which may,
of course, be given almost instantly, or, by a slower movement, the barrels
can be discharged at any required rate.
The barrels of the machine guns we have described do not, as is generally
supposed, radiate; on the contrary, they are arranged in a perfectly
parallel direction. In consequence of this, the bullets are at short ranges
directed nearly to one spot. The Gatling gun was adopted as a service
weapon by the British navy, and in several minor actions it had proved
effective, but in its original form it was superseded by the Gardner gun,
in which the barrels are fixed horizontally side by side, and are in number
five or fewer; each barrel is able to fire 120 rounds per minute. A new
system of feed was afterwards applied to the Gatling gun by Mr. Accles,
by means of which this gun was greatly improved and its rate of firing
was increased to more than 1,000 rounds per minute; indeed, 80 rounds
have been fired from it within 2 seconds. The Gatlings in this improved
form have ten barrels, and are provided with feed drums, each containing
104 cartridges, and capable, when empty, of being almost instantly
replaced by a full one. The contents of one drum can, if necessary, be
discharged in about 2¼ seconds, so that in this time 104 rifle bullets would
be fired; or considerably more than the rate of 1,000 rounds per minute
could easily be maintained. The weapon is so mounted, that without
moving its carriage it can be pointed at any angle of elevation or depression,
and through a considerable lateral range.
Mr. Nordenfelt has brought out a machine gun, which, on account of
224the simplicity and strength of its firing mechanism, has proved the most
reliable weapon of its class, and it also has been adopted into the British
service, and indeed into that of nearly every nation in the world. In
this gun there are five barrels arranged as in the Gardner, but the firing
is operated by a lever working backwards and forwards at the rate of
600 rounds per minute.
Fig. 105e.—A Hotchkiss Gun.
In the firing of all these weapons, by turning a crank, or moving a
lever at one side, any attempt at exact aiming must obviously be difficult
if not impossible, from the liability of the gun to get moved. Several
designs have been proposed for making the firing mechanism entirely
automatic so as to require no effort on the part of the firer, whose attention
can then be directed solely to pointing the piece. It would not be
225easy to explain in detail the way in which this is accomplished in these
very ingenious guns; for while the principle of their action is sufficiently
clear, namely, that the force of the recoil is made to extract the spent
cartridge, open the breech, insert a fresh cartridge, close the breech, and
fire the charge, the mechanism of the reacting springs, etc., by which this
is effected could scarcely, even by the aid of elaborate diagrams, be made
intelligible to any other than a gunsmith. The Maxim is one of those
automatic guns: it has but one barrel, and after the first discharge it
will go on firing with marvellous rapidity the cartridges supplied to it in
a continuous chain, and this without any deviation from such direction
as may be given to it by the operator, for he has neither crank to turn
nor lever to move, but merely sits behind an iron shield directing the
weapon at will, which, without interference, fires hundreds of shots per
minute from one barrel, so long as the long bands of cartridges are
supplied to it.
Mr. Nordenfelt and Mr. Hotchkiss have also both contrived quick
firing guns for 1–lb., 3–lb., and 6–lb. projectiles, and these, it has been
thought, will be of great service in naval warfare as against torpedo
boats.
Though the automatic mechanism, whereby the breech operations are
all performed by the force of the recoil of the barrel, which is allowed to
slide backwards, and is then returned to its place by a spring, is too
complicated for illustration here, mention may be made of a quite recent
device by which the recoil action is dispensed with, and the mechanism
so far simplified that scarcely more than half the number of parts in the
lock mechanism are required. Imagine a closed tube beneath the barrel,
parallel to it, and communicating with it only by a small boring near the
muzzle; through this opening the expanding gases will pass, in a degree
depending on its size and position, and by their action on a piston near
the breech, impulses are supplied that will actuate the lock mechanism so
long as cartridges are supplied, as they may be in a continuous band. A
weapon of this construction has been already tried, and its discharges are
so rapid that the sound of them is described as being quite deafening.
This plan appears to be equally applicable to small arms, and to machine
or field guns. A very effective gun of the kind, which fires ordinary rifle
bullets, has been contrived by Mr. Hotchkiss, and is represented in
Fig. 105e. It is capable of sending forth as many as 1,000 shots in one
minute.
Modern ordnance has required certain modifications in the making of
gunpowder, so that the original name of powder would now hardly be
applicable at all. The large charges now used, if introduced in the form
of fine powder, would certainly shatter the guns from the suddenness of
the exploding force. Hence the material is made up into larger or
smaller masses, generally rounded like small pebbles. The explosive
used for the huge 110–ton guns presents itself in the form of chocolate-coloured
hexagonal prisms, two or three inches long and about an inch
in diameter. These are obtained by compressing the specially prepared
material into moulds with a hydraulic press. The reason for this process
is that, in order to obtain precision and uniformity in the effects, not only
must the composition of the powder be always the same, but the size,
shape, weight, and number of the several portions that make up the
charge must be invariable. It has not been found possible to fire one of
these monster guns many times without such signs of deterioration as
226would suggest a short “life” for each of them. But the greatest necessity
for modern fire-arms is a smokeless powder or other explosive. It is
obvious that the advantages of quick firing, whether of large or of small
fire-arms, are greatly reduced if the soldier or gunner is prevented by
smoke from taking aim. The invention of a smokeless gunpowder has
several times been announced, and great advances have, indeed, been
made towards its realization. Certain compositions, which appeared to
meet the requirement of being practically smokeless, have, however,
been found liable to chemical changes, or to corrode the bore, or to
possess other objectionable properties. In this country the explosive
coming into use as best adapted for quick firing guns, etc., presents
itself in appearance like whitish or grey strings, and has hence received
the name of cordite. The composition and mode of manufacture of these
new substitutes for gunpowder are not readily disclosed, each military
authority jealously guarding its own secrets. The problem of smokeless
powder has, however, been almost completely solved, for at a military
review that took place on the Continent in 1889, the discharge of the
rifles (loaded with blank cartridges, of course) is said to have been
attended with no more smoke than the puff of a cigar. The new invention
will cause some changes in military tactics, for the manœuvres
formerly executed under cover of the battle smoke will no longer be
possible. Some particulars as to the nature of smokeless powders will
be found in the article on “Explosives.”
227
Fig. 106.—Harvey’s Torpedo. Working the Brakes.
TORPEDOES.
The notion of destroying ships or other structures by explosions of gunpowder,
contained in vessels made to float on the surface of the water,
or submerged beneath it, is not of very modern origin. Two hundred and
fifty years ago the English tried “floating petards” at the siege of Rochelle.
During the American War of Independence similar contrivances were used
against the British, and from time to time since then “torpedoes,” as they
were first termed by Fulton, have been employed in warfare in various
forms; but up to quite a recent period the use of torpedoes does not appear
to have been attended with any decided success, and it is probable that but
for the deplorable Civil War in the United States we should have heard
little of this invention. During that bitter fratricidal struggle, however,
when so much ingenuity was displayed in the contrivance of subsidiary
means of attack and defence, the torpedo came prominently into notice,
having been employed by the Confederates with the most marked effects.
It is said that thirty-nine Federal ships were blown up by Confederate
torpedoes, and the official reports own to twenty-five having been so
destroyed. This caused the American Government to turn their attention
to the torpedo, and they became so convinced of the importance of this
class of war engine that they built boats expressly for torpedo warfare, and
equipped six Monitors for the same purpose.
It has been well remarked that the torpedo plays the same part in naval
warfare as does the mine in operations by land. This exactly describes the
228purpose of the torpedo where it is used defensively, but the comparison
fails to suggest its capabilities as a weapon of offence. There are few occasions
where a mine is made the means of attack, while the torpedo readily
admits of such an employment, and, used in this way, it may become a
conspicuous feature of future naval engagements. Many forms of this war
engine have been invented, but all may be classified, in the first place, under
two heads: viz., stationary torpedoes, and mobile or offensive torpedoes;
while independent distinctions may be made according to the manner of
firing the charge; or, again, according to the mode of determining the
instant of the explosion. The stationary torpedo may be fixed to a pile or
a raft, or attached to a weight; the offensive torpedo may be either allowed
to float or drift against the hostile ships, or it may be propelled by machinery,
or attached to a spar of an ironclad or other vessel. The charge may be
fired by a match, by percussion, by friction, by electricity, or by some contrivance
for bringing chemicals into contact which act strongly upon each
other, and thus generate sufficient heat to ignite the charge. The instant
of explosion may be determined by the contact of the torpedo with the
hostile structure (in which case it is said to be “self-acting”), or by clockwork,
or at the will of persons directing the operations. In some cases lines
attached to triggers are employed; in others electric currents are made
use of.
Fig. 107.—Submerged Torpedo.
In the American Civil War the stationary torpedoes at first laid down
were self-acting, that is, they were so arranged as to explode when touched
by a passing vessel. Such arrangements present the great disadvantages
of being as dangerous to friendly as to hostile ships. The operation of
placing them is a perilous one, and when once sunk, they can only be
removed at great risk. Besides this, they cannot be relied on for certain
229action in time of need, as the self-acting apparatus is liable to get out of
order. The superiority of the method of firing them from the shore when
the proper instant arrived, became so obvious that the self-acting torpedo
was soon to a great extent superseded by one so arranged that an observer
could fire it at will, by means of a trigger-line or an electric current. Similar
plans had often been previously employed or suggested. For example,
during the war between Austria and Italy the Austrian engineers at Venice
had very large electric torpedoes sunk in the channels which form the approaches
to the city. They consisted of large wooden cases capable of containing
400 lbs. of gun-cotton, moored by chains to a wooden framework,
to which weights were lashed that sufficed to sink the whole apparatus,
Fig. 107. A cable containing insulated wires connected the torpedo with an
electrical arrangement on shore, and the explosion could take place only
by the operator sending a current through these wires. The torpedo was
wholly submerged, so that there was nothing visible to distinguish its position.
There was no need of a buoy or other mark, as in the case of self-acting
torpedoes, to warn friendly vessels off the dangerous spot, and therefore
nothing appeared to excite an enemy’s suspicions. But it is, however,
absolutely necessary that the defenders should know the precise position
of each of their submarine mines, so that they might explode it at the
moment the enemy’s ship came within the range of its destructive action.
This was accomplished at Venice in a highly ingenious manner, by erecting
a camera obscura in such a position that a complete picture of the protected
channels was projected on a fixed white table. While the torpedoes were
being placed in their positions an observer was stationed at the table, who
marked with a pencil the exact spot at which each torpedo was sunk into
the water. Further, those engaged in placing the torpedoes caused a small
boat to be rowed round the spot where the torpedo had been placed, so as
to describe a circle the radius of which corresponded to the limit of the
effective action of the torpedo. The course of the boat was traced on the
picture in the camera, so that a very accurate representation of the positions
of the submarine mines in the channels was obtained. Each circle
traced on the table was marked by a number, and the wire in connection
with the corresponding torpedo was led into the camera, and marked with
the same number, so that the observer stationed in the camera could, when
he saw the image of an enemy’s ship enter one of the circles, close the
electric circuit of the corresponding wire, and thus instantly explode the
proper torpedo. The events of the war did not afford an opportunity of
testing practically the efficiency of these preparations.
Another mode of exploding torpedoes from the shore has been devised
by Abel and Maury. It has the advantage of being applicable by night
as well as by day. The principle will be easily understood with the assistance
of the diagram, Fig. 108, in which, for the sake of simplicity, the
positions of only three torpedoes, 1, 2, 3, are represented.
Fig. 108.—Mode of Firing Torpedo.
In this arrangement two observers are required at different stations on
the shore. At each station—which should not, of course, be in any conspicuous
position—is a telescope, provided with a cross-wire, and capable
of turning horizontally about an upright axis. The telescope carries round
with it, over a circular table of non-conducting substance, a metallic pointer
which presses against narrow slips of metal let into the circumference of
the table. To each slip of metal a wire passing to a torpedo is attached,
and another wire is connected with the axis of the pointer, so as to be put
into electric contact with each of the others when the pointer touches the
230corresponding piece of metal on the rim of the table. The mode in which
these wires are connected with the torpedoes, the telescopes, and the electric
apparatus is shown by the lines in the diagram. At each station is a
key, which interrupts the electric circuit except when it is pressed down by
the operator. There are thus four different points at which contacts must
be simultaneously made before the circuit can be complete or a torpedo explode.
In the diagram three of these are represented as closed, and in such
a condition of affairs it only remains for the observer to depress the handle
of the key at station B to effect the explosion of torpedo No. 2. The observer
at station a is supposed to see the approaching vessel in the line of torpedo
No. 2, and recognizing this as an enemy’s ship, he depresses the key at his
station. The operator at B, by following the course of the vessel with his
telescope, will have brought the pointer into contact with the wire leading
to No. 2 torpedo, and he then causes the explosion to take place by completing
the circuit by depressing his key. A modification of this plan is
proposed by which the position of the torpedoes is indicated by placing
marks, such as differently-coloured flags, or by night lamps with coloured
glasses, throwing their light only towards the telescopes. These marks
are placed in the line of direction of each torpedo from the telescope as at
c1, c2, c3 and b1, b2 3; and if they can be put at some distance, the position
of the torpedo is determined with great accuracy by the intersection of
the lines of sight of the two telescopes. Electric wires connect the stations
and the torpedoes in the same manner as we have before described. Such
methods of firing torpedoes are no doubt the most efficient, for the destructive
charge may be sunk so far below the surface that not a ripple or an
eddy can excite an enemy’s suspicion, or the channel appear otherwise than
free and unobstructed, while friendly ships may pass and repass without
risk; for the current which determines the explosion only passes when the
two sentinels complete the circuit by simultaneously depressing their keys.
231Attempts have often been made to convert the torpedo into an offensive
weapon, by causing vessels containing explosive charges to drift by currents,
or otherwise, into contact with the enemy’s ships. The results have
been always unsatisfactory, as there is great uncertainty of the machine
coming into contact with its intended mark. Besides, it is easy to defend
vessels against such attacks by placing nets, &c., to intercept the hostile
visitors, especially if the attack is made by day, and by night the chance that
a torpedo drifting at random would strike its object is very small indeed.
One condition essential to the success of such attacks is that the approach
of the insidious antagonist may be unobserved. Accordingly divers schemes
have been projected for propelling vessels wholly submerged beneath the
surface of the water, so that they may approach their object unperceived,
and exert their destructive effect precisely at that part of the vessel where
damage is most fatal, and where an ironclad vessel is most vulnerable,
namely, below the water-line. Vessels have been built, propelled by steam
and so contrived that their bodies are wholly submerged, only the funnel
being visible above the surface. These quasi submarine ships carry small
crews, and are fitted with a long projecting spar in front, at the end of which
is carried the torpedo.
Fig. 109.—Explosion of Whitehead’s Torpedo.
Fig. 110.—Effect of the Explosion of Whitehead’s Torpedo.
The Federal navy sustained several disasters from torpedo-boats of this
kind. For example, the commander of the United States steamer Housatonic
reported the loss of that vessel by a rebel torpedo off Charleston on
the evening of the 17th February, 1864, stating that about 8·45 p.m. the
officer of the deck discovered something in the water about 100 yards from,
and moving towards, his ship. It had the appearance of a plank moving
in the water. It came directly towards the ship, the time from when it was
first seen till it was close alongside being about two minutes; and hardly
had it arrived close to the ship before it exploded, and the ship began to
sink. The torpedo-boat, with its commander and crew, were lost, having,
it is supposed, gone into the hole made by the explosion, and sunk with the
Housatonic. In general, however, the performance of submarine boats has
been unsatisfactory. There is the difficulty of determining accurately the
232course of the boat; there is great danger to the men manning it, as exemplified
in the case above; and there is again the problem of providing a
means of propulsion which shall enable such a boat to advance or retreat
for, say, a mile or more, without making its presence conspicuous by smoke
or otherwise. The latter condition would appear to exclude the use of
steam for such purposes, as the inevitable smoke and vapour would betray
the presence of the wily craft. Another power which has been proposed is
air strongly compressed, and recently a still more portable agent has been
suggested in solid carbonic acid, which is capable of exerting a pressure of
forty atmospheres by passing into the gaseous form. A locomotive form of
torpedo, invented by Mr. Whitehead, has the explosive charge, which consists
of about 18 lbs. of glyoxyline, placed in the front part of a cigar-shaped
vessel, the other part containing mechanism for working a screw-propeller,
by means of compressed air contained in a suitable reservoir. This torpedo
having been sunk a few feet below the water, the motive power may be set
in action by drawing a cord attached to a detent, when the mechanical fish
proceeds in a straight line under the water. It is said that this torpedo is
effective at 500 yards from the ship attacked, and may even be made sufficiently
powerful to travel 1,000 yards under the water. The great objection
to such arrangements is the uncertainty of the missile arriving at its destination,
for even supposing that the water were without currents, the least
deviation from the straight course would cause the torpedo to pass wide of
the mark at 1,000 yards distant. It is said that at the experimental trials
more than one projector of such war engines has been startled by his machine,
after pursuing a circuitous submarine course, exploding in dangerous
proximity to the place whence it was sent off, the engineer narrowly escaping
233being “hoist with his own petard.” The experiments which have been
made with Whitehead’s torpedo in smooth water appear, however, to have
been so far successful that we may probably hear of this invention being put
in practical operation in certain cases. Fig. 109 shows the upthrow of water
produced by the explosion of one of these torpedoes against an old hulk.
The large mass of water thus heaved up is a proof of the mechanical
energy of the explosion, and the effect on the hulk is shown in Fig. 110,
which exhibits the damage done to her timbers, from the effects of which, it
need hardly be said, she immediately sank. In Fig. 112 we have the representation
of the explosion of one of Whitehead’s torpedoes containing
67 lbs. of gun-cotton, instead of the glyoxyline. The accurate delineation
of these pyramids of water could not have been obtained but by the aid
of instantaneous photography, and it constitutes a good example of the
great value of such an application of that art, for the instantaneous photographs
obtained in these experiments enabled the engineers to calculate
accurately the volume and height of the column of water, which thus furnishes
a measure of the power of the explosion.
Fig. 111.—Experiment made by the Royal Engineers with a Torpedo charged with 10 lbs. of Gun-Cotton.
The ordinary torpedo adopted by the British authorities for coast defence
consists of a cylinder of boiler plate, 4 ft. long and 3 ft. in diameter. It is
intended to contain 432 lbs. of loose gun-cotton, equivalent in explosive
energy to about a ton of gunpowder. The effect of one of these torpedoes
exploded 37 ft. beneath the surface of the water is depicted in Fig. 113,
234and in Fig. 114 is shown the effect produced when the same charge was
exploded at the depth of 27 ft. below the surface. Gun-cotton appears to
be the most effective explosive for torpedoes, if we may judge by the large
volume of water heaved up, as witness Fig. 111, which shows the result with
a small torpedo, containing only 10 lbs. of gun-cotton, exploded at a less
depth than those already mentioned. The ordinary torpedoes are moored
by an anchor attached to the torpedo, and floating above it is a buoy shaped
like an inverted cone. This cone contains a mechanical arrangement of
such a nature that when it is struck by a passing vessel, an electric circuit
is closed by bringing into contact two wires connecting the torpedo with a
voltaic battery on shore. While the apparatus may thus be at any moment
made fatal to a hostile vessel touching it, from the control it is under by the
engineer having the management of the battery contacts, friendly vessels
may pass over it with impunity.
Fig. 112.—Explosion of Whitehead’s Torpedo, containing 67 lbs. of Gun-Cotton.
The employment of torpedoes develops, as a matter of course, a system
of defence against them. Nets spread across a channel will catch drifting
torpedoes, and stationary ones may be caused to explode harmlessly by
nets attached to spars pushed a great distance forward from the advancing
ship.
Before the final adoption of Whitehead’s torpedo, presently to be
described, the British Government had, after various official trials,
approved of a towing torpedo designed for offensive operations. It is
the invention of Commander Harvey, and is worthy of a detailed
description for the ingenuity of its construction.
Fig. 113.—Explosion of 432 lbs. of Gun-Cotton in 37 feet of Water.
Fig. 114.—Explosion of 432 lbs. of Gun-Cotton in 27 feet of Water.
The shape of Harvey’s torpedo, as may be noticed on reference to Fig.
118, is not symmetrical, but it has some remote resemblance to a boat,
though constructed with flat surfaces throughout. The outside case is
formed of wood well bound with iron, all the joints being made thoroughly
water-tight. The length is 5 ft. and the depth 1¾ ft., while the breadth is
only 6 in. Within this wooden case is another water-tight case made of
235thick sheet copper, from the top of which two very short wide tubes pass
upwards to what we may term the deck of the wooden case. These are
the apertures through which the charge of gunpowder or other explosive
material is introduced; and when the tubes have been securely stopped
with corks, brass caps are screwed on. The centre of the internal case is
occupied by a copper tube, g, Fig. 115, which passes the entire depth, and
is soldered to the top and bottom of the copper case, so that the interior of
the tube has no communication with the body of the torpedo, the principal
charge merely surrounding it. Thus the tube forms a small and quite independent
chamber in the midst of the large one, which latter is capable
of containing 80 lbs. of gunpowder. The copper tube or priming-case contains
also a charge, a, which when exploded bursts the tube, and thus fires
the torpedo in its centre. The priming charge is put in from the lower
end of the tube, which is afterwards closed by a cork and brass cap, h;
236for the centre of the priming-case is occupied by a brass tube, b, closed at
the bottom, but having within a pointed steel pin projecting upwards. In
this tube works the exploding bolt c d, which requires a pressure of 30 or
40 lbs. to force it down upon the steel pin. This pressure is communicated
to the bolt by the straight lever working in the slot at its head, d, and
itself acted on at its extremity by the curved lever to which it is attached.
Thus from the mechanical advantage at
which the levers act a moderate downward
pressure suffices to force the exploding bolt
to the bottom of the brass tube. The lower
end of this bolt has a cavity containing an
exploding composition sufficient in itself
to fire the torpedo, even independently of
the priming charge contained in the copper
tube. This composition is safely retained
in the end of the bolt by a metallic capsule,
c, which, when the bolt is forced down,
is pierced through by the steel pin at the
bottom of the brass tube, and then the explosion
takes place. The bolts are not
liable to explosion by concussion or exposure
to moderate heat, and they can be
kept for an indefinite period without deterioration.
Fig. 115.—Section of Priming-Case and Exploding Bolt.
The mode of producing the explosion is
not stated: it consists probably of an
arrangement for bringing chemicals into
contact. Besides the two levers already
mentioned, a shorter curved lever working
horizontally will be noticed. The object
of this is to make a lateral pressure also
effective in forcing down the bolt—a result
accomplished by attaching to the short
arm of the lever a greased cord, which,
after passing horizontally through a fairleader,
runs through an eye (see Fig. 117) in the straight lever, and has
its extremity fastened so that a horizontal movement of the short lever
draws the other down. A very important part of the apparatus is the
safety key, f, Fig. 115, a wedge which passes through a slot in the exploding
bolt, and resting on the brass-work of the priming-case, retains the muzzle
1 in. above the pin. Through the eye of the safety key and round the
bolts passes a piece of packthread, e, which being knotted is strong enough
to keep the key securely in its place, but weak enough to yield when the
strain is put on the line, d´, used for withdrawing the safety key at the proper
moment. This line is attached to the eye of the key, and passes through
one of the handles forming the termination of the iron straps. As represented
in Fig. 117, it forms the centre one of the three coils of rope. The
bottom of the torpedo is ballasted with an iron plate, to which several
thicknesses of sheet lead can be screwed on as occasion requires. Fig. 117
shows the arrangement of the slings by which the torpedo is attached to
the tow-rope, and it will be seen that another rope passes backwards
through an eye in the stern to the spindle-shaped object behind the torpedo.
This is a buoy, of which two at least are always used, although only
237one is represented in the figure. Each buoy, in length 4½ ft., is made of
solid layers of cork built up on an iron tube running through it lengthways,
so that the buoys admit of being strung upon the rope.
Fig. 116.—Harvey’s Torpedo.
Having thus described the construction of the torpedo, we proceed to
explain how it is used. It must be understood that if the torpedo and its
attached buoys are left stationary in the water, the tow-rope being quite
slack, the torpedo will, from its own weight, sink several feet below the
surface. But when they are towed, the strain upon the tow-line brings the
torpedo to the surface, to dip below it again as often as the tow-line is
slackened. There is another peculiarity in the behaviour of the torpedo,
and that is that, when towed, it does not follow in the wake of the vessel,
but diverges from the ship’s track to the extent of 45°. Its shape and the
mode in which it is attached to the tow-line are designed so as to obtain
this divergence. But, according as the torpedo is required to diverge to the
right or to the left, there must be the corresponding shape and arrangement
of tow-line and levers; hence two forms of torpedo are required, the starboard
and the port. The figures represent the port torpedo, or that which
is launched from the left side of the torpedo-ship, and diverges to the left of
its course. The efficiency of the torpedo depends upon the readiness and
certainty with which it can be brought into contact with the hostile ship,
and this is accomplished by duly arranging the course of the torpedo
vessel, and by skilfully regulating the tow-line so as to obtain the requisite
amount of divergence, and to cause the torpedo to strike at the proper
depth. The tow-rope is wound on a reel, furnished with a powerful brake,
the action of which will be readily understood by inspection of Fig. 116,
238which represents also a similar smaller reel for the line attached to the
safety key. Leather straps, sprinkled with rosin to increase the friction,
encircle the drums of the reels, and can be made to embrace them tightly
by means of levers, so that the running out of the lines can be checked as
quickly as may be desired. Handles are attached to the straps, so that
they can be lifted off the drum when the line is being drawn in by working
the handles. When the torpedo is ready for action and has been launched,
a suitable length of tow-line, which is marked with knots every ten fathoms,
is allowed to run off its reel, while the safety key-line is at the same time
run off the small reel, care being taken to avoid fouling or such strains
on the line as would prematurely withdraw the key. Fig. 106 will make
clear the mode of controlling the lines, but it is not intended to represent
the actual disposition in practice, where the men and the brakes would be
placed under cover. On the left of the figure a starboard torpedo is about
to be launched; on the right a port torpedo has been drawn under the ironclad
and is in the act of exploding, the safety key having been withdrawn
by winding in its line when the torpedo came into proximity to the attacked
vessel.
Fig. 117.—Harvey’s Torpedo.
Fig. 118.—Harvey’s Torpedo.
Fig. 119.—Official Trial of “Harvey’s Sea Torpedo,” February, 1870.
When the torpedo has been launched over the vessel’s side, the latter
being in motion, the torpedo immediately diverges clear of the ship; and
when the buoys have also reached the water, the men working the reels
pay out the line steadily, occasionally checking the torpedo to keep it near
the surface, but avoiding a sudden strain upon the slacked tow-rope, which
would cause the torpedo to dive, and in shallow water this might lead to
the injury or loss of the torpedo. The torpedo can be gradually veered out
to the distance required, at the same time that the safety-key is so managed
that sufficient strain may be put upon it to prevent it from forming a long
239bight astern of the torpedo, but avoiding such a strain as would break the
yarn holding the safety-key in its place. The distance to which the tow-line
may be paid will depend upon the circumstances of the attack. More
than 50 fathoms is, however, a disadvantage, as the long bight of tow-lines
makes the torpedo drag astern. The torpedo can always be made to
dive several feet below the surface by suddenly letting out two or three
fathoms of tow-line. The torpedo vessel should, of course, be a steamer of
240considerable speed—able to outstrip when necessary all her antagonists,
and, as a rule, it is found best to make the attack at night. Let us imagine
two ships of war at anchor, and parallel to each other at perhaps a distance
of 60 fathoms; and suppose that, under cover of darkness, a hostile torpedo
vessel boldly steams up between them, having launched both its
starboard and port torpedoes. In such a case neither ship could fire at the
torpedo vessel for fear of injuring the other, while the torpedo vessel would
in all probability succeed in bringing its floating mines into contact with
both its enemies.
Fig. 120.—Model of Submarine Guns.
Another device for submarine attacks upon vessels on which much ingenuity
has been expended is the submarine gun. It has been sought to
propel missiles beneath the surface of the water, these missiles being usually
provided with a charge which, on contact with the vessel’s side, would explode,
and by making a hole below the water-line, cause the certain destruction
of the ship. It is obvious that such a mode of attack would reach the
only vulnerable parts of a thickly-plated ironclad, and therefore the project
has been recently revived in several forms. Fig. 120 is taken from the photograph
of a model of an invention of this kind. The guns which are to propel
the submarine projectiles, have port-holes formed by valves in such a manner
that the gun when loaded can be run out without allowing water to enter;
it can then be fired while the muzzle is below the surface, and again drawn
in without the port being at any time so opened that water can pour into
the vessel. All contrivances of this kind have hitherto been failures; indeed,
it does not appear possible that they could succeed, except at very close
quarters, for the resistance offered by water to a body moving rapidly in it
is extremely great, and, as we have already had occasion to state, the resistance
increases as the square of the velocity, and probably in even a higher
degree for very great velocities. Any one who will remember the effort it
241requires to move one’s hand quickly backwards and forwards through
water will easily understand that the resistance it presents would, in a comparatively
short space, check the speed of a projectile, however great that
speed might be at first. A good many years ago Mr. Warner produced
a great sensation by an invention which appears to have been essentially
a floating torpedo. The cut below, Fig. 121, represents the result of
an experiment publicly made by him off Brighton, in 1844, upon a barque,
which was towed out by a steamer to a distance of a mile and a half from
the shore. Mr. Warner was on board the steamer, and the barque was
300 yards astern. Five minutes after a signal had been made from the
shore, the torpedo was caused to explode, striking the barque amidships,
throwing up a large column of water and débris, shooting the mainmast
clean out of the vessel, the mizen going by the board, and dividing the hull
into two parts, so that she sank immediately. Yet this invention, though
apparently so successful, does not seem to have ever been put in practice.
Fig. 121.—The Warner Experiment off Brighton.
The stationary torpedoes of the kind mostly used in the American
Civil War were, as already stated, self-acting; that is, they exploded
when touched by a passing vessel. They would now be more generally
called self-acting mines, and are to be distinguished from that form of the
weapon in which the explosion is determined by some manipulation on
shore, such as the closing of an electric circuit, when the hostile vessel
comes within the area of destructive action. This form receives the
name of observation mines. Stationary mines are essentially instruments
of defence, and as such are employed for the protection of rivers and
harbours. The self-acting varieties usually contain a charge of 70 lbs. to
24280 lbs. of gun-cotton, and are commonly arranged in lines. Of course,
when the occasion for which such mines have been laid down is past, they
must be removed, and the operation of picking them up is one of great
danger. The observation mines, on the other hand, do not require immediate
removal, and they can be taken up with little risk. In the
British service the observation mine contains about 500 lbs. of gun-cotton,
and a line of these is sometimes moored in a water-way, from 35
feet to 50 feet below the surface. The area of destructive action in this
case is a circle of about 30 feet radius, and therefore a line of seven such
mines laid across a channel at intervals of 120 feet apart would ensure
the almost certain destruction of any war vessel of ordinary breadth that
might attempt to pass up a river of 840 feet in width. This is about the
distance across the Thames near the Tower of London, but the depth of
the river there being only 12 feet at low-water and 33 feet at high-water,
would not suffice to give effect to the full energy of so large a charge of
gun-cotton; for it has been found that, for a given charge, there is a
certain depth under water at which its explosion will produce the
maximum effect, and this depth will be greater with heavier charges than
with light ones. The regulation “observation mine” of the British service
has a cylindrical case of stout plate-iron, 32 inches in diameter and 34
inches high, with domed ends. Within this gun-cotton is contained, in a wet
condition, in a number of copper envelopes, which have holes for access of
water to wet the charge from time to time as occasion requires, the wet
condition being the safest for the carriage of gun-cotton. The centre of
the case is a tin charged with some discs of dry gun-cotton, and the
detonator required to bring about the explosion of the whole charge when
the electrical contact is made, fires the fuze contained within the primer.
These cases are arranged to have a certain buoyancy, and are moored
with wire ropes to heavy iron sinkers, the mooring ropes being of such
length as to keep the explosive case at the proper depth below the surface,
and of sufficient strength to resist the force of the currents in the waterway.
There is also another type of submarine mine, operated by an
electric current, the circuit of which is closed by contact of a passing
vessel, if at the time a battery on shore is included in the circuit. In this
way the mines can be made harmless or dangerous for passing vessels at
the will of the operator on shore. The passing vessel is made to complete
the circuit by tilting over the cylindrical case so far that some
mercury contained in a small part of it is upset, and makes the requisite
metallic contact. This arrangement is known as the electro-contact mine.
In former pages of this article on torpedoes will be found representations
of the effects produced by Whitehead’s torpedo, which, being
automobile and travelling altogether under the surface of the water, was
capable of being made a very formidable weapon of offence. When the
earlier editions of this work were going through the press, it was understood
that the Whitehead torpedo left much to be desired as regards
speed, certainty of direction through the water, and perhaps in other
points, the inventor being constantly engaged in effecting improvements.
At that time particular pains were taken to keep secret the nature of the
most important parts of the internal mechanism. The work of construction
was carried on in a room with locked doors, blocked-out windows,
and a military guard outside. The earlier experimental forms of this
automobile torpedo were constructed in complete secrecy by the inventor
himself, with the help of only one trusted, skilled mechanic and a boy,
243who was no other than Mr. Whitehead’s own son. The history of the
invention is very interesting, and exemplifies the power of skill and
perseverance to overcome a multitude of difficulties, the result being a
machine which is simply a marvel of ingenuity and of delicate nicety of
adaptation.
The first notion of the automobile torpedo appears to have occurred to
an Austrian naval officer; but it took rather the form of a small vessel
containing within itself some propelling power by which it could move
along the surface of the water, its course being directed by ropes or
guiding lines from the shore or from a ship. The fore part of the little
vessel was to hold an explosive, to be fired automatically by the self-propelled
torpedo coming into contact with the side of the hostile vessel.
The propelling power, as first suggested, was clockwork, if that could be
made efficient, or steam as an alternative. The Austrian authorities,
however, considered that it would be impracticable to direct the course of
the torpedo in the manner proposed, and that there were also great
objections to each of the methods of obtaining motive power. The
assistance of a thoroughly competent and skilful mechanician was then
sought, and Mr. Whitehead, at that time the director of an engineering
establishment at Fiume, devoted himself to solving the problem of devising
a torpedo which should be able to travel beneath the surface of the
water, and, when once started, should require no external guidance to keep
it on its proper course. After some years of experimental labours, Mr.
Whitehead produced the first form of the weapon with which his name is
associated, but to this he has since added from time to time many ingenious
improvements. A committee of experts having been appointed
by the Austrian Government to test the capabilities of the new invention,
it was made the subject of a long series of trials, after which the committee
recommended its immediate adoption in the Austrian navy. The
earlier form of the Whitehead torpedo had, however, the defect already
mentioned, of being sometimes very erratic in its course; its speed was
small (6 knots) compared with that of the more recent patterns (30 knots),
and its range of travel proportionately less. The British Admiralty
having invited Mr. Whitehead to visit England with some specimens of
his invention, a committee was appointed to make complete trials of the
capabilities of two weapons he had brought with him. Although by this
time great improvements had been made on the original design, and in
particular, Mr. Whitehead had almost completely overcome the difficulty
of keeping the torpedo at a uniform depth during its course, by means of
delicate adjustments in what we may call the steering chamber (to be
presently mentioned), much remained to be accomplished before the
weapon attained the perfection of the modern patterns. Indeed, the
inventor may be said to have from time to time redesigned his contrivances,
as when in 1876 the speed was increased to 18 knots, and again in
1884 more powerful engines brought up the speed to 24 knots. Further
improvements have been made by Mr. Whitehead, who designed a new
form of the weapon in 1889, and some of the more recent patterns can
now show a speed of 30 knots or more. The committee appointed by
the Admiralty to conduct experiments with the first pair of torpedoes
brought to England, after having tested them in various ways for a period
extending over six months, reported that they believed that “any maritime
nation failing to provide itself with submarine locomotive torpedoes,
would be neglecting a great source of power, both for offence and defence.”
244Upon this recommendation the Admiralty immediately purchased
from Mr. Whitehead for £15,000 the secret of the internal
mechanism of his invention and the rights of manufacturing it. The
self-adjusting apparatus within the steering chamber, by means of which
the torpedo was kept at its due depth, was then a jealously-guarded
secret; but when the arrangement with Mr. Whitehead was effected, the
Government immediately set about the manufacture of these torpedoes on
a large scale. The artificers employed in making the Whitehead torpedoes
were now numerous, and the internal structure of these weapons
could not advantageously be altogether concealed from those who had to
handle them on board of the ships, so that it inevitably happened that
some details of their construction leaked out, and came into the possession
of other powers, whereupon all the maritime states followed the example
of Great Britain by providing their navies with Whitehead or some such
form of locomotive torpedo. It is no part of our plan to enter into the
mechanical minutiæ of the Whitehead torpedo. We may, however, give
the reader such an idea of the external appearance and internal arrangement
of the Whitehead torpedo as will enable him to appreciate to some
extent the ingenuity and skill that have been brought to bear upon its
construction.
There are in existence many different patterns of the weapon—twenty-four,
it is said—and this is what might be expected from the fact of its being
produced at several different manufactories, each striving to effect whatever
improvements its resources will supply. Some torpedoes have been
made at Fiume, very many at Mr. Whitehead’s works at Portland, as also
at the Government establishment at Woolwich, while private enterprise
in this direction is encouraged by contracts with some private firms, such
as that of Messrs. Greenwood & Bately at Leeds. The greatest diameter
of the large torpedo is 18 inches, but in some it is rather more, in others
14 inches or 16 inches; and the length may vary between 14 feet and
19 feet. Many of our Whitehead torpedoes are made of polished steel,
but in the later patterns phosphor-bronze is partly made use of, as being
not liable to corrode. The interior of the torpedo is divided by transverse
partitions into five distinct compartments. The foremost of these, called
the “head,” contains the explosive charge when the weapon is ready for
use in actual warfare. This section, which may occupy about one-sixth
of the total length, is an air-tight case made of phosphor-bronze, one-sixteenth
of an inch thick, and it is kept permanently charged with slabs
of wet gun-cotton, which may amount to 200 pounds weight in all, and is
ready to be attached by a screw and bayonet joint to the body of the
torpedo; but this is done only at the time immediately before it is
required for its destructive employment. Its place at other times, as
when the torpedo is used for drill practice, and to test its running powers,
is occupied by a dummy head of steel, of exactly the same shape and
size, and packed with wood in such a manner that its weight and centre
of gravity are like those of the explosive head when the latter is ready for
action. The wet gun-cotton requires a detonative explosive of dry
material close to it, in order to determine its own detonation. The explosive
heads of the Whitehead are not fitted with the pistol and priming
tube until all is ready for the discharge of the weapon, as this would
render the handling of the torpedo highly dangerous. This priming
apparatus is merely a metallic tube that slips into a corresponding hollow
in the explosive head so far as to reach well within the wet gun-cotton
245charge, although still separated from the latter by a metal casing. The
posterior extremity of the priming tube contains a few ounces of dry gun-cotton,
and just in front of this is a copper cap containing some fulminate
of mercury, which readily explodes when struck by the point of a steel rod,
occupying the centre of the tube and projecting a short distance out at
the “nose” of the torpedo, so as to be driven inwards by the impact of
the latter on a ship’s side. The explosion of the fulminate causes the detonation
of the dry gun-cotton at the bottom of the priming tube, and this
is taken up by the whole mass of the explosive with destructive effect.
The danger of premature or accidental explosion by anything coming in
contact with the projecting striker is obviated by several checks which
prevent any chance blow driving the rod home against the fulminate
charge. The anterior projecting end of the rod has a screw thread
worked upon it, and on this turns freely a nut provided with wings like a
small fan, revolving in such a manner that as the torpedo is moved
through the water, the nut is spun off, and the striker is free to be driven
back, except in so far as it is still retained by a small copper pin, the
breaking of which requires a considerable blow. Again, the little fan
above mentioned cannot begin to spin off the rod until another pin or
wedge has been withdrawn, which operation is performed just before
launching the weapon.
Immediately behind the exploding head of the torpedo is the air-chamber,
which occupies a considerable space in the length, i.e., about
one-third of the whole. This part is made of the toughest steel, nearly ⅓
of an inch thick, and contains the power actuating the motor, in the form
of air forced into it by powerful pumps on board the ship, until the
pressure reaches the enormous amount of 1,300 lbs. or more on the square
inch, or, at least, this is what is made use of in the newer patterns when
charged for action. In the largest size of the weapon the weight of air
injected may be more than 60 lbs., and, of course, considerably detracts
from the buoyancy of this part.
Behind the air-chamber comes another much shorter compartment we
have called the “steering chamber,” in which are contained the most ingenious
and delicate parts of the apparatus, namely, the mechanism by
which this extraordinary artificial fish adjusts itself, after the manner of a
living thing, to the required conditions. Among other contrivances, it
contains several valves controlling the action of the compressed air on
the engines, etc. The enormous pressure to which the air-chamber is
charged, if allowed to act unchecked, would give at first a power almost
sufficient to shatter the machinery, and, in order to prevent this, a “reducing
valve” is interposed so that only a moderate and uniform pressure
of air is allowed to act upon the engines. Then there is the “starting
valve” by which the air is admitted or cut off from the engines, and still
another valve which is contrived to delay the action of the compressed
air for the short interval during which the torpedo is passing from the
discharging tube until it enters the water. For during this interval the
propellers not having to act against the water, but only against the resistance
of the atmosphere, would be whirled round at an enormous speed,
and the machinery would sustain such shocks and strains as might endanger
the whole apparatus. It is to prevent this that the “delay action
valve” is provided.
The automatic apparatus by which the torpedo’s course is regulated is
a very remarkable part of the invention, and it admits of the nicest adjustments.
246This was the crown of Mr. Whitehead’s ingenuity, but the
details were, by an arrangement between the government and the inventor,
not to be made public, though necessarily communicated to certain officers
in the service, and known to the chief artisans employed in their fabrication.
These persons are all, we believe, required to give pledges not to
divulge the arrangement of particular parts. But such details could
scarcely be made intelligible, even should they be interesting, to the
general reader. The principles upon which the controlling apparatus are
arranged may, however, be comprehended without difficulty.
The tail of the torpedo is provided with two rudders, one in its central
vertical plane, and the other in its central horizontal plane. Their action
in directing the torpedo’s course is exactly that which the tail supplies to
a fish, or the rudder to a boat. Suppose that while the torpedo is passing
through the water the vertical rudder is by any means turned towards one
side, the course of the metallic fish will be diverted towards that side; or
again, a turning upwards of the horizontal rudder would have the effect of
directing the nose towards the surface, and would make the torpedo rise,
and so on. Now the positions of the horizontal rudder are regulated from
the “steering chamber,” in which a heavy weight is suspended like
a pendulum, so as to be capable of swinging fore and aft. This
pendulous weight actuates the horizontal rudder through a system
of rods and levers, so that when it hangs vertically the horizontal
rudder is level, but if from any cause the nose of the torpedo were directed
downwards, the pendulous weight would come to a more forward position
in the steering chamber, and would raise the rudder, and thus turn the
nose towards the surface until the original horizontal position were regained.
In the contrary case, of course, the reverse action would take
place. But the torpedo, while preserving a horizontal position, might tend
to sink to too great a depth, or rise too near the surface, and this is prevented
by another adjustment, namely, a piston receiving the pressure of
the water, which, on the other side, is opposed by a spring. If the
torpedo sinks a little the pressure increases, the piston, which moves with
perfect freedom without allowing water to pass in, is forced inwards, and
its movement is communicated to the same levers that connect the pendulous
weight with the horizontal rudder, the latter is raised, and then the
nose of the torpedo is directed upwards, and it consequently approaches
the surface again. In the contrary case the spring, relieved from some of
the external pressure, operates the levers in the other direction.
The compartment immediately behind the “steering chamber” contains
the engines which are of the Brotherhood type, provided with three single
acting cylinders. The three-fold throw prevents any possibility of the
engine getting on a “dead point.” Though this compartment is the
shortest in the torpedo, the engines in the larger sizes are capable of indicating
as much as thirty horse power. It has for simplicity been stated
above that the pendulous weight and the balanced piston act by means of
rods on the horizontal rudder; this was so in the early patterns of the
torpedo, but it was soon found that they did not do so with sufficient steadiness
and promptitude, and the force they could apply was in the larger
and swifter forms quite ineffective. Nowadays the engine compartment
always contains a little piece of apparatus which is an arrangement of
cylinder and piston, upon which the compressed air acts in one or the
other direction according to the way its slide-valve is moved. It is this
slide-valve that the rods from the “steering chamber” move, and allow
247the force of the compressed air to turn the rudder up or down. This
auxiliary apparatus has the same relation to the torpedo rudder that the
steam-steering apparatus of a large vessel has to its rudder. Although it
is only about a few inches long, its power and delicacy are such that the
pressure of half an ounce on its slide admits to its piston a force equal to
160 lbs., and its introduction has given the torpedo the power of steadily
steering itself.
Behind the engine compartment, but completely shut off from it, is another
almost empty division occupying a considerable part of the length
of the torpedo, and known as the “buoyancy chamber.” But it contains,
attached to the bottom of it, a certain amount of ballasting, so adjusted
to balance the weights of the other parts that the whole floats horizontally,
and at the same time preserving the tube in one vertical position as regards
its transverse diameter, i.e., so that the horizontal rudder is always
horizontal. The shaft from the engine passes through this compartment,
as also the rod from the small motor that moves the horizontal rudder.
These, of course, pass through water-tight bearings.
At the tail of the torpedo, behind the rudders, are two three-bladed
screw propellers, of which the anterior one is mounted on a tubular shaft
having a common axis with the other, but made to revolve in the opposite
direction by means of a bevel wheel mounted on each independent shaft,
with a third such wheel connecting them. The object of the double screw
is to obviate “slip,” that is, ineffective motion of the blades through the
water, and by this means the full power of the engines can be developed;
while any tendency to deviation to right or left, due to the rotation, is reduced
to a minimum. We have spoken of one horizontal and one vertical
rudder, although externally there appear to be two of each kind, right and
left, above and below, on the tail of the torpedo. These pairs, however,
are so connected as to be always in the same respective planes. The
controlling mechanism acting in two different ways on the horizontal
rudder has been already indicated, but nothing has yet been said about
the vertical rudder. It is not moveable by anything within the torpedo,
but is commonly fixed by clamping screws in or about the same vertical
plane as the axis of the torpedo, and it performs the same function as a
kind of back fin, which, in the earlier forms, extended nearly the whole
length of the tube; and that is obviating any tendency of the torpedo to
roll about its axis. The vertical rudder can also be fixed at a considerable
inclination to the axis should occasion require, and the effect of that would
be to cause the torpedo to pursue a circular course of greater or less
radius, according to the less or greater degree of inclination. Very rarely,
however, would this be required, and the vertical rudder may be considered
as fixed in the axial plane, or having such slight inclination as
may, on trial, have been found necessary to counteract any tendency to
lateral deviation.
There are several different methods for discharging the Whitehead
torpedoes from ships. They may be sent from a tube below the water-line,
but the arrangements for that purpose are complicated and difficult
to manage, while, on the other hand, the launch of the weapon is not perceived
by the enemy, and it is at the same time out of the reach of any
blow from a hostile missile while yet in its discharging tube. More commonly
the discharging tube is arranged above the water-level. On
regular torpedo boats, the tubes are sometimes mounted on pairs upon a
revolving table, provided with many nice adjustments, and even the
248single above-water torpedo tube, as used between decks, is an apparatus
having somewhat complicated appliances. The torpedo is expelled from
the tube now preferably by a small charge of cordite. But in the Royal
Navy no fewer than some twenty different patterns of torpedo tubes have
been in use for the various sizes of torpedoes. In some of these, compressed
air, in others gunpowder or cordite, in others, again, mechanical
impulse propels the torpedo into its element. It would obviously be impossible
within our limits to enter into details of these various constructions,
or to attempt descriptions of all the ingenious contrivances applied
to the torpedo itself, or to give an account of the means of defence against
mines and torpedoes, this last being a matter belonging to naval tactics.
The adoption of the torpedo as a naval weapon has given rise to special
types of boats adapted for its employment, and these again have required
other boats to destroy them (“torpedo-boat destroyers” or “catchers”).
Light draught and high speed were desired in these last; but in many
cases the intended speed was inferior to that of the torpedo boats that
were to be caught.
The following particulars about the British torpedo-boat destroyer
Daring may be compared with those given of the cruiser Majestic. The
Daring is 185 feet long, 7 broad, and she draws only 7 feet of water.
Her speed is about 28½ knots per hour, with a steam pressure in the
boilers of 200 lbs. per square inch, and an air pressure in the stoke-holds
equivalent to 3 inches of water (forced draught.)
The importance attached to the prospective use in war of the automobile
torpedo may be shown by the fact that at the end of 1890 the
number of torpedo boats built or laid down for England was 206, and for
France 210, while other nations followed with numbers proportionate to
their means. Forty “torpedo-boat destroyers” were in building for the
British Navy towards the close of the year 1896, and now (March, 1897)
it is announced that the number of torpedo boats and torpedo-boat
destroyers in the French Navy is to be increased by 175.
249
Fig. 122.—M. Ferdinand de Lesseps.
SHIP CANALS. — THE SUEZ CANAL. — THE MANCHESTER SHIP CANAL. — THE NORTH SEA CANAL. — THE PANAMA AND NICARAGUA CANAL PROJECTS.
Artificial canals are amongst the oldest of inventions, for,
centuries ago, they have been constructed, even of very large dimensions,
in various parts of the world. There is in China, for instance, a
great canal, 900 miles in length and 200 feet broad, which is supposed to
have been made 800 years ago. The advantages of canals did not escape
the attention of the Egyptians, Greeks and Romans. We read of very
early attempts to cut through isthmuses, in order to form a water communication
between regions where other carriage would be long and
difficult. It appears to be admitted that canals connecting the Red Sea
with the Mediterranean existed some centuries before the Christian era,
and to cut the Isthmus of Corinth by a waterway was a cherished project
with several Roman Emperors, and now it appears that in this nineteenth
century this project will shortly be realized. But as the canal-lock is but
a comparatively modern invention, dating only from the fourteenth
century, and first used in Holland, all the canals anterior to that period
had to be designed as level cuts, a restriction which greatly increased the
difficulties of the problem. Canals were in use in various parts of Europe,
250particularly in Holland and France, long before any were constructed in
England, as, for example, the Languedoc Canal, which, by a cut of 150
miles, connects the Bay of Biscay with the Mediterranean. It is 60 feet
broad, and attains, at its highest level, an elevation of 600 feet above the
sea. The canal system in England was first introduced in the middle of
the eighteenth century, and soon afterwards, the Duke of Bridgewater
engaged the famous Brindley to construct a canal, connecting his collieries
at Worsley with Manchester, about seven miles distant, and afterwards
extended his scheme, so as to open up a more direct water communication
between Manchester and Liverpool. Before the making of this canal,
the cost of the carriage of goods between these towns had been forty
shillings per ton by land, and twelve shillings by water. After that, they
were conveyed with regularity for six shillings per ton. The system was
soon extended, so as to connect the Trent with the Mersey, and the boldness
of both the projectors and their engineer in carrying out this scheme
is memorable in the history of such undertakings. Brindley was equal
to the task of coping with the difficulty of carrying his canal over what
had hitherto been supposed an insuperable obstacle, for he pierced Harecastle
Hill with a tunnel more than a mile and a half in length—a then
unheard of piece of engineering—to say nothing of several shorter tunnels,
many aqueducts, and scores of locks. The Duke of Bridgewater, who at
one period had been unable to raise £500 on his own bond for the
prosecution of his scheme, died in 1803, in receipt of a princely income
from the profits of his useful undertaking. For its creation, he had,
however, denied himself the present enjoyments of his patrimonial
revenue, by reducing his expenses at one period to the modest sum of
£400 per annum. Before his death, the Duke, for taxation purposes,
estimated his income at £110,000 per annum. Before the railway system
was fully established a network of canals had united the most populous
places in England, the total length of the waterways being not much less
than two thousand miles. With the rise of railways the importance of
canals as channels for the conveyance of merchandise declined. But,
nevertheless, in consequence of the continued increase of traffic and the
great cheapness with which goods can be carried by water, canals are
often able to compete with railways in the carriage of bulky or heavy
goods when speed of transit is not an object. The English canals have,
therefore, never been disused or abandoned, notwithstanding the
ubiquitous ramifications of the railway lines. Nay, the value of the
Bridgewater Canal system, about to be superseded so far as concerns the
communication between Liverpool and Manchester by the greater
scheme we have presently to describe, is such that £1,710,000 is now
required for its purchase; and that is the value in spite of four lines of
railway connecting those great towns, and all competing for the carriage
of goods. In these canals, designed for inland communication only, the
navigation is confined to boats or barges of very insignificant dimensions
compared with the sea-going ships that some great modern canals
are constructed to receive.
To the present century belongs the famous “Caledonian Canal,” as the
waterway is often called that extends in a straight line for more than
60 miles across Scotland, in north-east and south-west directions.
The canal work here was commenced in 1802, under the direction of
Telford, and though it was opened for traffic in 1822, the work as it now
exists was not completed until 1847. But the length of the actual canal
251construction in this case did not much exceed 23 miles, for a
natural waterway, navigable for ships of any burden, is formed by the
series of narrow lakes that fill what is called the “Great Glen of the
Highlands.” This glen has many of the characteristics of a great artificial
ditch: its highest point is only 90 feet above the tide level in
Loch Linnhe; a circumstance not a little remarkable in so mountainous
a country. What is also remarkable is the great depth of these lakes,
which in some places exceeds 900 feet. The banks also are
generally very steep, and indeed at one time it was impracticable to pass
along the shores of Loch Ness, the longest of the lakes. But there are
now good roads along both banks. Although the ground traversed by
the artificial channels of the Caledonian Canal is chiefly alluvial, the cost
of the undertaking proved to be great, amounting, it is said, to about one
and a quarter million pounds sterling. Indeed, had it not been for the
introduction of steam navigation before the completion of the work, and
the consequent increase and facility of water conveyance, it is doubtful
whether the utility of this canal would have been commensurate with its
cost, or its receipts have made any profit for its promoters. By the
Caledonian Canal large steamers and other vessels may pass from sea to
sea, and in the summer time the steamers that traverse it are crowded
with tourists attracted by the magnificent scenery it presents throughout
the greater part of its length.
But whatever had previously been done in canal construction was surpassed
in enterprise and importance by Lesseps’ great work in Egypt.
As we have already seen, the idea of opening a waterway between the Red
Sea and the Mediterranean is by no means a product of the present
century. The ancient Egyptians do not appear to have cut directly
through the Isthmus, but Herodotus describes a canal made by Necho
about the year 600 B.C., from Suez through the Bitter Lakes to Lake
Timsah and then westward to Bubastis on the Nile. He mentions
certain water gates, and states that vessels took four days in sailing
through. This canal became silted up with sand ages ago, but it was
cleared out again and re-opened in the seventh century of our era by the
Caliph Omar, and traces of it are still visible. According to some recent
discoveries in the chief archives of Venice, as early as the end of the
fifteenth century, when Vasco da Gama had discovered the Cape of
Good Hope, and the Portuguese took that new route to India, hitherto the
exclusive property of the Venetian and Genoese merchants, a re-cutting
of the Isthmus of Suez was thought of. Plans were prepared and
embassies sent to Egypt for paving the way for the accomplishment of
this great enterprise, which, it is said, was only foiled by the persistent
opposition of some patricians, who were probably bribed by foreign gold
to prevent the execution of the plan. One of our Elizabethan poets,
Christopher Marlowe, appears, in the following lines, to have anticipated
M. de Lesseps:—
“Thence marched I into Egypt and Arabia,
And here, not far from Alexandria,
Whereat the Terrene and the Red Sea meet,
Being distant less than full a hundred leagues.
I meant to cut a channel to them both,
That men might quickly sail to India.”
252For at that period travellers going to India in the famous sailing ships,
called “East Indiamen,” were obliged to sail round the Cape of Good
Hope and pass from the Southern to the Indian Ocean. The reader who
wishes to understand the importance of the Suez Canal should look at the
map of the Eastern Hemisphere, where he will have no difficulty in
finding the position of the vast continent of Africa, which is washed on
the north by the Mediterranean Sea, on the west by the Atlantic, on the
south by the Southern Ocean, and on the east and north-east by the
Indian Ocean and the Red Sea. If he now traces the waterway round
Africa, on coming to the head of the Red Sea he will find the only
interruption of the oceanic continuity in the narrow neck of land called
the Isthmus of Suez. But for this, ships might long ago have made
complete circuits round this vast, and, even as yet, but partially explored
continent. The circuit would, indeed, be a great one of some 15,000
miles; but the barrier that the Isthmus presented to inter-oceanic communication
between the eastern and the western worlds was a piece of
physical geography which has undoubtedly been a most important factor
in determining the course of history. It has been said that had there
existed at Suez a strait like that of Gibraltar or that of Messina, instead
of a sandy isthmus, the achievements of Diaz, Vasco da Gama, and
Columbus would have lost much of their significance; but the advantages
to the world’s commerce would have been incalculable, and the progress
of the race might have been more rapid.
The Emperor Napoleon I. had the idea of restoring the old canal; but
it was only when steam navigation had taken its place on the seas that
the scheme was looked upon as offering any chance of financial success.
But General Chesney, who made some surveys for the French Government
in 1830, had come to the conclusion that there was a considerable
difference of level between the two seas—a difference, he calculated, of
about 30 feet. The existence of such a state of things would, of course,
have been very unfavourable for the undertaking; but the General’s
supposition was soon proved to have been erroneous.
The suggestion of carrying out the project of constructing a ship
canal through the Isthmus was seriously revived by Père Enfantin, the
St. Simonian, in the year 1833. He then induced M. Ferdinand Lesseps,
the French vice-consul, and Mehemet Ali, the Pasha of Egypt, to take
some practical measures towards its accomplishment. Surveys were
made, but owing to the breaking out of a plague, and to other causes, not
much more was heard of the scheme till 1845. In 1846 La Société
d’Etude du Canal de Suez was formed, and among those who turned
their attention to the subject was Robert Stephenson. His report was
wholly unfavourable to the enterprise. He recommended the construction
of a railway through Egypt, and a line was accordingly made between
Alexandria and Suez. But, notwithstanding the opinion of Mr. Stephenson,
M. Lesseps persevered with wonderful energy, believing, on the
report of other engineers, that the scheme could be successfully carried
out. It is right, however, to state that Mr. Stephenson did not say it
was impossible to complete the Suez Canal—he merely gave it as his
opinion that the cost of making the canal, and keeping it in a proper state
for navigation, would be so great that the scheme would not pay. However,
in 1854, the Viceroy of Egypt signed the concession, and in 1860
the work was actually commenced, but not on a plan that was advocated
by the English engineers of making the canal 25 feet above the sea level.
253There were also some political and financial difficulties to be overcome.
The Suez Canal Company, it was said, had expended twelve millions of
money in what was considered to be chiefly shifting sands.
Fig. 123.—The Sand-Glass.
When the Suez Canal was projected, many prophesied evil to the undertaking,
from the sand of the Desert being drifted by the wind into the
canal, and others were apprehensive that where the canal was cut through
the sand, the bottom would be pushed up by the pressure of the banks.
They imagined that the sand would behave exactly like the ooze of a soft
peat-bog, through which, when a trench has been cut, the bottom of the
trench soon rises, for the soft matter has virtually the properties of a
liquid: it acts, in fact, exactly like very thick treacle.
Sand, however, is not possessed of liquid properties;
it has a definite angle of repose, which is not the
case with thin bog. This behaviour of sand is
familiarly illustrated in the sand-glass, which the
diagram Fig. 123, will recall to mind. It may be
observed that the sand falling in a slender stream
from the upper compartment is in the lower one
heaped up in a little mound, the sides of which
preserve a nearly constant inclination of about 30°.
In this property it is distinctly different from peat-bog
or such-like material, which has no definite
angle of repose. It need hardly be said that all
apprehensions as to the safety of the canal from the
causes here alluded to have proved unfounded.
But if some English engineers appeared to oppose
the project, another eminent one, Mr. Hawkshaw,
certainly helped it on at a moment when the
Viceroy of Egypt was losing confidence; and, had
his opinion been adverse to the project reported
upon, the Viceroy would certainly not have taken
upon himself additional liability in connection with the undertaking,
and the money expended up to that date would have been represented
only by some huge mounds of sand and many shiploads of artificial
stone, thrown into the bottom of the sea to make the harbour of Port
Saïd. And that M. Lesseps appreciated the good offices of Mr. Hawkshaw
is shown from the fact that, when he introduced that engineer to
various distinguished persons, on the occasion of the opening of the canal,
he said, “This is the gentleman to whom I owe the canal.” It cannot,
therefore, be said of the English nation that they were jealous of the
peaceful work of their French neighbours, or opposed it in any other
sense but as a “non-paying” and apparently unprofitable scheme.
The Canal was opened in great state by Napoleon III.’s Empress
Eugénie, in November, 1869, when a fleet of fifty vessels passed through,
and the fact was thus officially announced in Paris:—“The canal has
been traversed from end to end without hindrance, and the Imperial yacht,
Aigle, after a splendid passage, now lies at her moorings in the Red
Sea.
“Thus are realized the hopes which were entertained of this great
undertaking—the joining of the two seas.
“The Government of the Emperor cannot but look with satisfaction
upon the success of an enterprise which it has never ceased to encourage.
A work like this, successfully accomplished in the face of so many
254obstacles, does honour to the energetic initiative of the French mind, and
is a testimony to the progress of modern science.”
An Imperial decree was then issued, dated the 19th of November,
appointing M. de Lesseps to the rank of Grand Cross of the Legion of
Honour, in consideration of his services in piercing the Isthmus of Suez.
The Suez Canal is 88 geographical, or about 100 statute miles long: its
average width is 25 yards, and the minimum depth, 26 feet. At intervals
of five or six miles, the canal is widened, for a short space, to 50 yards,
forming thus sidings (gares) where only vessels can pass each other. At
these, therefore, a ship has often to wait until a file of perhaps twenty
steamers, coming the other way, has passed. Occasionally a ship gets
across, or “touches,” and then the canal is blocked for hours. So much
inconvenience has been found from the restricted dimensions of the work,
that in 1886 it was proposed to widen the canal, or, alternatively, to construct
a second canal, and use the two like the lines of a railway, so that
vessels would never have occasion to pass each other. The amount of
traffic is very large, and has been steadily increasing. Thus, in 1874, the
tonnage of the vessels passing through was 5,794,400 tons; in 1880, the
tonnage was 8,183,313, and the receipts of the Company amounted to
£2,309,218. In 1875, the British Government purchased, from the Khedive,
£4,000,000 worth of shares.
Fig. 124.—A Group of Egyptian Fellahs, and their Wives.
The Suez Canal is not so much a triumph of engineering as a monument
of successful enterprise and determination on the part of its great promoter,
M. Lesseps, in the face of great difficulties. According to the original
programme, the canal was to have been constructed by forced labour,
supplied by the Viceroy. The unhappy peasantry of the country, called
“fellahs,” were compelled to give their labour for a miserable pittance of
rice. No doubt, in ancient times, when forced labour was in use, every
peasant might cheerfully work, because it was for the general benefit to
bring sweet water from the Nile to other dry and thirsty places in Egypt;
but to be obliged to work at a waterway of salt, which was only to be of
255use to foreigners who passed through the country, could not be expected
of human beings, and therefore the carrying out of the work was not
unaccompanied by cruelties of the nature attending slave labour in other
lands. This was one of the reasons why the late Lord Palmerston opposed
the canal scheme, for the kind hearted statesman bore in mind the loss
of health and life occasioned to poor Egyptians by this mode of labour,
and the more so because it had been originally proposed that one of the
conditions on which the French Company was to take up the project should
be the execution of the work by free labour. In consequence, no doubt,
of representations from free countries, the Porte was induced to put a
veto on the employment of forced labour, and everyone thought that this
would be the deathblow to the completion of the canal: but M. Lesseps
did not give way to despair, and he since stated that if he had depended
on the labours of the fellahs only, the difficulties of the work never could
have been surmounted; and that, in fact, the successful prosecution of
the work was owing to his having turned his attention to the mechanical
contrivances used for dredging on the Thames and the Clyde, from
which he obtained better results in half the time and at half the cost.
Fig. 125.—Dredges and Elevators at Work.
Fig. 126.—Map of the Suez Canal.
The dredges used in the construction of the canal were of a new description.
They were wonderful mechanical contrivances, and but for
them the canal would not have been finished. They were not the
contrivance of M. Lesseps, but of one of the contractors, a distinguished
engineer, who received his technical education in France but his practical
experience in England. The use of the dredging machines was prepared for
by digging out a rough trough by spade work, and as soon as it had been
dug to the depth of from six feet to twelve feet, the water was let in. After
the water had been let in, the steam dredges were floated down the
stream, moored along the bank, and set to work. The dredges were of
two kinds. The great couloirs consisted of a long, broad, flat bottomed
barge, on which stood a huge framework of wood, supporting an endless
chain of heavy iron buckets. The chain was turned by steam, and the
height of the axle was shifted from time to time, so that the empty
buckets, as they revolved round and round, should always strike
the bottom of the canal at a fixed angle. As they were dragged
256over the soil they scooped up a quantity
of mud and sand and water, and as
each bucket reached its highest point
in the round, it discharged its contents
into a long iron pipe which ran out
at right angles to the barge. The
further extremity of this pipe stretched
for some yards beyond the bank of
the canal, and therefore, when the
dredging was going on, there was a
constant stream of liquid mud pouring
from the pipe’s mouth upon the shore,
and thus raising the height of the
embankment. When the hollow
scooped out by the buckets had
reached the required depth, the dredge
was moved to another place, and the
same process was repeated over and
over again. These stationary dredges,
however, though very effective, required
much time in moving, and the
lighter work of the canal was chiefly
effected by movable dredges of a
smaller size. These machines were
of the same construction as those described;
the only difference was that
the mud raised by their agency was
not poured directly on shore by pipes
attached to the dredges, but was
emptied in the first instance into large
barges moored alongside the dredge.
These barges were divided into compartments,
each of which contained a
railway truck, and when the barge was
filled it steered away to the bank,
where an elevator was fixed. The
trucks, filled with mud were raised by
a crane worked by steam power, and
placed upon inclined rails, attached
to the elevator, which sloped upwards
at an angle of 45 degrees towards the
bank. They were then drawn up the
rails by an endless rope, and as each
truck reached the end of the rails its
side fell open, the mud was shot out
upon the bank, and the empty truck
returned by another set of rails to the
platform on which the elevator was
placed, and was thence lowered into
the barge to which it belonged. As
the elevator could unload and re-load
a barge much faster than the dredges
could fill it with mud, each elevator
257was fed by half a dozen dredges, and thus the mud raised from the canal
by several dredges was carted away without difficulty at one and the
same time. As these floating dredges were much easier to shift than
those encumbered by the long couloir pipes, the work of excavating the
bed went on much more rapidly. But in places where there was any
great mass of earth or sand to be removed, the large couloirs could
scoop out a given volume in a shorter time.
The traveller who wishes to see the canal should go to France, and,
embarking at the port of Marseilles, cross the Mediterranean Sea, and
steam to Port Saïd, which is about 150 miles east of the port of Alexandria,
where the isthmus is crossed by the railroad, and is used by
travellers to India, being known as the “overland route.” And this
railway conveys the mail to and from India, thus saving the great sea
voyage round Africa and the Cape of Good Hope. Nevertheless, it
involves two transhipments—from the steamer to the rail at Alexandria,
and from the railway to the steamer at Suez.
Fig. 127.—Port Saïd, the Mediterranean entrance to the Suez Canal.
Let us notice in order the places passed by the traveller in going from Port
Saïd to Suez and the Red Sea. The arrow (Fig. 126) points in the direction
of the compass, and shows that the canal runs very nearly from north to
south. Port Saïd is the little town at the northern or Mediterranean entrance
to the canal, situated on the flat sands at the entrance of the canal,
and is built chiefly of wood, with straight wide streets and houses, and
although it now contains several thousand inhabitants, before the
making of the canal was begun one hundred people could hardly have
been got together. The town contains nothing deserving of notice, and
has a striking resemblance to the newly settled cities of America. But in
it reside agents who represent numerous varied interests—administrative,
financial, mercantile and political. It is provided with docks, basins,
quays and warehouses, and has a harbour stretching out a couple of miles
or so into the sea, for to that distance two piers, or rather breakwaters,
run out.
258Fig. 128 shows these two converging breakwaters, which have been
built out into the Mediterranean from the coast, the larger and more
westerly one being one mile and a half long, the shorter about a mile and
a quarter, and the distances between the two lighthouses erected on the
extremities of the breakwater being half a mile.
The piers are made of concrete which was cast in blocks weighing
10 tons each. This composition has of late years been greatly approved
by engineers where stone cannot be procured. The sea-face of the great
canal in Holland is composed of a similar artificial stone, and it is found
to bear the wear and tear of the waves almost, if not quite, as well as
ordinary stone. It is stated that 25,000 blocks, each weighing 10 tons,
were used. They were not laid with the regularity of ordinary masonry,
but had been dropped from large barges, so that they presented a very
rugged and uneven appearance (Fig. 129); but the object of throwing out
these great bulwarks is for the purpose of preventing the sand brought
down by the Nile silting in and closing up the canal. Along the western
pier there is, from this cause, a constant settlement of sand, which was
partially washed through the interstices left between the blocks of artificial
stone, and might have given some trouble by forming sandbanks
in the harbour; but this was prevented by the introduction of smaller
stones, which could readily be carried out in boats at the low tide.
Fig. 128.—Bird’s-eye View of Port Saïd.
Beginning with the Mediterranean Sea and Port Saïd, there is a run
of 28 miles to Kantara, through Lake Menzaleh. Although called a
lake, it is, in truth, nothing but a shallow lagoon or swamp, in which
water-fowl of all kinds are very abundant, the great flocks of white pelicans
and pink flamingoes being especially striking. The waters of this
259lagoon cover lands that once were fertile, and the salt sea-sands doubtless
conceal the remains of many an ancient town.
Fig. 129.—One of the Breakwaters at Port Saïd.
Of all portions of the undertaking, this one, M. Lesseps states, was
the most arduous and difficult, though, at the time, it attracted the least
attention. A trough had to be dredged out of the bed of the shallow
lagoon, and on either side of this hollowed out space high sandbanks
had to be erected, and the difficulty of making a solid foundation for
these sand banks was found to be extreme. The difficulty, however, was
surmounted, and such is the excellence of the work, that the water neither
leaks out, nor does any of the brackish water of the lagoon infiltrate and
undermine the great embankments.
Fig. 130.—Lake Timsah and Ismaïlia.
At Kantara, the canal crosses the track of the highway between Cairo
and Syria—a floating bridge carries the caravans across; and near this
spot is stationed an Egyptian man-of-war, which supplies the police for
the proper watch and ward of the canal. From Kantara to El Fendane
is a distance of 15 miles—that is to say, to the southern extremity of Lake
260Ballah, where the canal still passes through sand embankments, raised
within a mere. The lake is, however, almost dried up, and therefore the
difficulties which had to be surmounted at Lake Menzaleh were not felt
here.
The traveller may now be supposed to have arrived at Lake Timsah,
where, no doubt, in the days of the Pharaohs, a lake existed. When taken
in hand by M. Lesseps, it was a barren, sandy hollow, containing a few
shallow pools, through which a man could easily wade, but now it is filled
with the waters of the Mediterranean Sea. It is a pretty, inland, salt
water lake, about three miles in width. On the northern shore stands the
town, or, rather, small settlement of Ismaïlia, which is, in fact, the “half
way house” where most of the officials of the Suez Canal Company resided,
as they could get to either end of the canal with greater facility, or to
Cairo by the railroad, which comes to this point, and continues, with the
canal, to Suez.
Fig. 131.—Railway Station at Ismaïlia.
When the canal was opened, in November, 1869, Ismaïlia was the scene
of the most brilliant part of the opening ceremony, in which the French
Empress Eugénie, the Empress of Austria, the Crown Prince of Prussia,
and other distinguished personages took share. The Khedive built himself
a summer palace, and M. Lesseps erected a villa, and the town was
most artistically laid out, with every prospect of becoming a flourishing
place. But the drainage had been so entirely overlooked, that it is said
the sewage found its only outlet in the fresh water canal; and the consequence
was fever broke out and so infected the town, that it was soon
almost quite deserted. In 1882, Ismaïlia was once more the scene of
bustle and activity, for here was the base of Sir Garnet Wolseley’s operations
in his brilliant campaign against Arabi. The British Navy entered
the canal, and took possession of Ismaïlia, where the army and the military
stores were rapidly concentrated. From this place, Sir Garnet advanced
along the route of the railway and the Sweet Water Canal, and, after
storming the lines of Tel-el-Kebir, occupied Cairo, without further resistance,
after a campaign of only three weeks’ duration.
From Lake Timsah to the Bitter Lakes the canal again passes for eight
miles or so through the desert, where, by partial excavations by hand
labour and subsequent flooding to admit the dredges, it was considered
261that a sufficiently deep channel could be made. The couloirs were set to
work, when suddenly “a lion arose in their path” in the shape of a great
rock, about 80 feet in length, and lying 12 feet only below the
surface, and right in the middle of the main channel. If anything could
show the indomitable energy of M. Lesseps it was his courage in dealing
with this difficulty, and at a time when a few months only could elapse
before the advertised day of the opening. He attacked the sunken rock
with gunpowder. A large raft, or floor, supported on barges, was moored
over the sunken rock, and from this men, armed with long poles shod
with steel, drilled numerous holes, into which charges of gunpowder were
placed, and fired in the usual manner by the electric battery. This temporary
obstruction occurred opposite to the landing place at Sérápeum.
Fig. 132.—The Viceroy of Egypt cutting the last embankment of the Reservoir of the Plain of Suez, to unite the two seas—the Mediterranean and the Red Sea.
Passing by Sérápeum, the traveller arrives at a vast expanse of water
called the “Bitter Lakes,” because the dry sandy hollow formerly contained
a marsh, or mere, of very brackish water. The possibility of
keeping this great area filled with sea water had been denied by the
opponents of the canal, who said the water would sink into the sand or be
evaporated by the intense heat of the sun; but none of these prognostications
have been verified, and it is now a great inland sea, far
surpassing Lake Timsah, being 25 miles long and from six to
seven miles wide. The only difficulty in filling this enormous natural
basin arose from the rapidity and force with which the waters flowed in.
This was done when the water at Suez was at low tide, and then subsequently
the Red Sea was allowed to flow in. Though the expanse of
water in the Bitter Lakes is great enough, the available channel is still
narrow. But the steamers can proceed at full speed, as here there are
no banks to be washed away.
Since the two seas have joined their waters, a strong current has set in
from south to north, but there is no eddy or fall at the place where the
262waters meet. The tide runs up the canal with great force, and there is a
difference of six or seven feet between high and low water: but the tide
does not extend beyond the Bitter Lakes, where it is gradually diffused
and lost. The colour of the current of water from Suez is said to be
green, whilst that portion fed by the Mediterranean is blue. Since the
Bitter Lakes have been filled the mean temperature of the districts on
the banks has fallen 5° Centigrade. It is also stated that, although the
canal swarms with sea fish they keep to their respective ends of the
canal, as if the Mediterranean fish would not consort with those of the
Red Sea, or, rather, make themselves at home in strange waters. There
is also, perhaps, another cause, and that is the very bitter nature of the
water at the northern end of the Bitter Lakes, which acts as a natural
barrier, through which the fish may decline to pass.
The bed of the Bitter Lakes is the only portion of the canal’s course
in which it was not necessary to make a cutting. Buoys are laid down
to mark the best channel, but such is the width and depth of the water
that vessels need not exactly keep within them. Quitting the Bitter
Lakes we again enter the canal proper. In order to reach the vast docks
which the Suez Canal Company has constructed on the western coast of the
Red Sea, the canal is now quitted, and the vessel crosses the neck of the
Red Sea. The Cairo and Alexandria Railway has been extended two
miles, and is carried through the sea on an embankment, which lands
the train close to the docks and quays of the canal, so that passengers by
the overland route are able to embark from the train on board the
steamer, and thus escape the troublesome transhipment of themselves
and luggage.
The project of constructing a ship canal to connect Manchester with
the sea appears to have been started just before the railway era, but
it was then abandoned, as the opening of the Liverpool and Manchester
Canal brought about an immediate reduction in the rates of carriage.
Perhaps it was the success of the Suez Canal which caused the revival of
this scheme, in 1880, combined with the depression of the cotton trade at
that period, when the Liverpool dock dues and the comparatively high
railway rates proved a heavier tax than usual on the great Lancashire
industry. The first definite steps were taken two years afterwards, when
two plans were submitted for the selection of a committee. One scheme
proposed to construct the canal without any locks; but, as Manchester
is 60 feet above the sea level, there would, it was felt, be certain inconveniences
in loading or unloading ships in a deep depression. The other
plan was submitted by Mr. Leader Williams, a well known canal engineer,
who proposed to take the canal from Runcorn, a distance of 20 miles,
and making use of locks. When Parliament was applied to for powers
authorizing the prosecution of the enterprise, there was, of course, much
opposition offered by the various interests involved, and the inquires
before the Committees of each House of Parliament were unusually protracted,
for they extended in all to 175 days, and the cost to the promoters
is said to have amounted to £150,000. Then, when the Bill had
passed, it was found that the capital (£8,000,000) could not be raised owing
to the financial depression, and partly also to some want of confidence in
264the soundness of the undertaking on the part of the Lancashire capitalists.
But the promoters submitted the whole scheme to a representative committee,
who should consider any possible objections. This committee
reported (after sitting almost daily for five weeks) upon every point, and
were unanimous in pronouncing the undertaking to be perfectly practicable
and commercially sound. After this there was no difficulty in
raising the required capital, which was subscribed by corporate bodies as
well as private persons. The contract was let for £5,750,000, and the
work was commenced in November, 1887, the contractor undertaking to
have the canal completed and ready for traffic by January 1st, 1892.
Fig. 133.—Western Portion.
Fig. 134.—Eastern Portion.
Figs. 133 and 134.—Map of the Manchester Ship Canal.
The Manchester Docks of this canal will cover an area of nearly 200
acres at the south-western suburb of that city, and from there the canal
traverses the Valley of the Irwell, following, indeed, the general course of
the river, but not its windings, so that the bed of the river is, in the distance
of eight miles, or down to its junction with the Mersey, repeatedly
crossed by the line of the canal. From the confluence of the rivers, the
canal traverses the Valley of the Mersey, for this is the name retained by
the combined streams. The course of the river, in its progress towards
the sea, now makes wider bends, but the canal proceeds, by a slight and
nearly uniform curve, to Latchford, near Warrington, passing to the
south of which last named place it follows a straight line to Runcorn,
which is at a distance of 23 miles from Manchester. Here it
reaches what is now the estuary of the Mersey, but the embankments
are continued along the southern shore to Eastham, where the terminal
locks are placed. In this part of the canal, the engineer had difficulties to
overcome of a different nature from those encountered in the upper part,
where it was chiefly a matter of cutting across the ground intervening
between the bends of the river, so as to form for its waters a new and
direct channel everywhere of the requisite breadth and depth. But when
Runcorn has been passed, and Weston Point rounded, there is the mouth
of the River Weaver to be crossed, and this is marked by a great expanse
of loose and shifting mud. Other affluents of the Mersey are dealt with
by means of sluices, and in one instance the waters of a river are actually
carried beneath the course of the canal by conduits of 12 feet in
diameter. The total length of the canal from Manchester to the tidal
locks at Eastham is 35 miles.
Fig. 135.—A Cutting for the Manchester Ship Canal.
Fig. 136.—Blasting Rocks for the Manchester Ship Canal.
The minimum width of the canal at the bottom is 120 feet, its depth
26 feet. But for several miles below Manchester this width will be
increased, so that ships may be moored along the sides, and yet sufficient
space left for the up and down lines of traffic in the middle. In this way,
works and manufactories on the banks will be able to load and unload
their cargoes at their own doors, and it may be expected that the advantages
so offered will cause the banks of the canal to be much in request for the
sites of works of all kinds. At the several places where the locks are
placed there will be a smaller and a larger one, side by side, so that water
shall not be needlessly used in passing a moderate sized vessel through
the greater locks. As these last are 550 feet long and 60 feet wide, they are
capable of receiving the largest ships, whilst the smaller locks are 300 feet
long and 40 feet wide. Again, both the larger and the smaller are provided
with gates in the middle, so that only half their length may be used when
that is found sufficient. Coming down the canal from Manchester, the
first set of locks will be at Barton, about three miles distance, just below
the place where the Bridgewater Canal is carried across the Irwell, which
266is now to become the ship canal, by means of the aqueduct of 1760, by
which Brindley became so famous. There is a story told about Brindley
being desirous of satisfying the duke about the practicability of his plan,
and requesting the confirmatory opinion of another engineer. When,
however, this gentleman was taken to the place where it was proposed to
construct the aqueduct, he shook his head, and said that he had often
heard of castles in the air, but had never before been shown where any of
them were to be erected. This aqueduct is about 600 feet long, and the
central one of its three arches spans the river at a height of nearly 40 feet
above the water. But the Manchester Ship Canal requires a clear headway
of 75 feet, and Mr. Williams is going to replace the fixed stone
structure by a swinging aqueduct, or trough of iron, which can be turned
round, so as to give a clear passage for ships in his canal. This trough,
or great iron box, will have gates at each end, and gates will be provided
in the aqueduct at each side, so that no water will be lost when the water
bridge is turned aside. But more than this; hydraulic lifts have been
designed, so that, in a few minutes, vessels can be lowered from the
Bridgewater Canal into the Manchester Canal, or raised from the latter
into the former while still floating in water. The supply of water for the
canal will be ample, as it has the rivers Irwell, Mersey and Bollin, with
their tributary streams, to draw from. It should be mentioned that the
terminal locks at Eastham will be of somewhat larger dimensions than
those already referred to, and will be three in number. The largest,
267which is on the south or landward side, will be 600 feet by 80 feet, the
middle one 350 feet by 50 feet, and the smallest one 150 feet by 30 feet.
These three locks will be separated by concrete piers 30 feet wide, on
which will be placed the hydraulic machinery for opening and closing the
gates. Besides the ordinary gates, there will be provided for each lock
at Eastham an outer pair of storm-gates that will be closed only in rough
weather. These gates will shut from the outside against the lock sills,
and, by resisting the force of wind and waves, will protect the ordinary
tidal gates from being forced open. The lock gates throughout will be
made of a wood obtained from British Guiana, and known as greenheart.
This timber is the product of a large tree (Nectandra Rodiœi) belonging
to the laurel family. It is a very heavy and close grained wood, the
strength and endurance of which have been proved many years ago by its
use in ship-building, etc., and some of the logs imported for the canal are
remarkably fine specimens, being 22 inches square and 60 feet long. A
pair of the largest gates weigh about 500 tons. The gates of the tidal
locks at Eastham will all be open for half the time of each tide, when
there will be a depth of water, above the sills, greater by 11 feet than that
of any dock in Liverpool or Birkenhead.
Fig. 137.—Manchester Ship Canal Works, Runcorn.
The way in which the difficulty is overcome of crossing the several
busy lines of railway that intersect the course of the new canal, so that
their traffic shall not be impeded, is one of special interest in this bold
scheme. The London and North Western Railway crosses the Mersey
268at Runcorn by a bridge that leaves a clear headway of 75 feet at high
water, and it was determined that this headway should be maintained in
the bridges over the canal. The use of swing bridges on lines of railway
over which trains are constantly passing being out of the question, it is
necessary that the railways be carried over the canal at the required
height. It is accordingly laid down in the Act of Parliament that before
the Canal Company can cut the existing lines of railway it shall construct
permanent bridges, and carry over them lines rising by gradients not
exceeding 1 in 135, and not only so, but these deviation lines must be
previously given up to the several railway companies for six months to
be tried experimentally in that period for goods traffic. The cost of
constructing these deviation lines, which, in all, will not be far short of
12 miles of new railway, will not be much less than £500,000. The
traffic of the canal will probably have great feeders at certain points in
the other canals and the railway lines that reach it. For instance, the
Bridgewater Canal, now incorporated with the greater undertaking, will
bring traffic from the Staffordshire potteries, the river Weaver brings salt
laden barges from Cheshire, and at other points the railways will bring
the produce of the excellent coal fields of South Yorkshire and South
Lancashire, which will be automatically transferred from the waggons
into ocean going steamships.
Fig. 137a.—The French Steam Navvy.
Fig. 137b.—The English Steam Navvy.
Though the general notion of the construction of the canal as a deep,
wide trench, or cutting following the course shown on the map, is
sufficiently simple, the operation of carrying this into practice involves
the exercise of great skill and ingenuity in dealing with mechanical
269obstacles. Man’s operations in the world consist but in changing the
position of masses of matter; and the properties of matter—its inertia,
cohesion, gravitation, etc., are the forces that oppose his efforts. The
quantity of matter to be shifted in excavating this trench of thirty-five
miles long across the country was no less than sixty millions of tons. The
number of “navvies” employed at one time has been 15,000; but even
this army of workmen would have made but slow progress with a cutting
of this magnitude, had not the “strong shouldered steam” been also
called into operation for scooping out the soil. The illustrations (Figs.
137a and #137b:fig137b) will show the arrangement of two forms of “steam
navvies” that were much used on the works. One (Fig. 137a) is similar
to the dredgers used for clearing mud out of rivers and canals: it consists
of a series of scoops, or buckets, mounted on an endless chain, so as to
scrape the material from an inclined embankment and tip it into waggons
for removal. The other (Fig. 137b) may be compared to a gigantic ladle
made to scrape against the face of a cutting in rising, and filling each
time its bucket with nearly a ton of the material. It is most interesting
to witness the perfect control which the man at the levers exercises over
this machine, the movements of which he directs with as much precision
as if he were handling a spoon. One of these steam navvies is able to
270fill 600 waggons or more—that is, to remove 3,000 tons of material—in
one day; and as many as eighty of them have been simultaneously used
on the Canal works. The value of the plant employed by the contractor
is estimated at £700,000, and the length of temporary railway lines (see
Fig. 137), for transport of the “spoil,” etc., is said to exceed 200 miles.
There is a main line running through from one end of the canal to the
other, and known to the workmen as the “Overland Route.” From this
diverge numerous branches, some to the bottom of the excavations in
progress, others to embankments down which is tipped out the “spoil,”
as the dug out material is called; while others connecting with brickfields
and quarries, or with existing canals and railway lines, serve to bring
supplies of the materials used in the constructions. Some 150 locomotives
are constantly at work on these temporary lines, and the coal consumed
by them, and by the steam navvies, steam cranes, pumping
engines, etc., is equivalent to about two train loads every day.
Though the Manchester Ship Canal is to be nearly twice as wide as
the Suez Canal, its width for some miles below Manchester will be still
greater, for there the banks will form long continuous wharves for the
accommodation of the works and factories that are certain to be attracted
to the spot. Indeed, so obvious are the advantages of ocean shipment,
and so extensive the industries of South Lancashire, that it is not improbable
the whole course of the canal may, in process of time, be lined
with wharves, and the two great cities of Manchester and Liverpool may
be united by a continuous track of dense population. Be that as it may,
there seems every reason to believe that the undertaking will be a financial
success. Calculation has shown that if the cotton alone that enters and
leaves Manchester were carried by the canal at half the rates charged by
the railways, there would result not only an annual saving of £456,000 to
the cotton trade, but a clear profit to the canal company sufficient to pay
more than 3 per cent. interest on its own capital. And, again, the railway
and other local interests that have hitherto been opposed to this
great enterprise can hardly fail to be in the long run benefited by the
enlarged prosperity and increased general trade and manufactures it will
develop. So that it will presently be found that there is room enough
and work enough for both canal and railways.
The Manchester Ship Canal, so far from having been ready for traffic
on the 1st January, 1892, was not completed until the end of 1893, and it
was only on the 16th December, 1893, that the directors and their friends
made the trial trip throughout its entire length, accomplishing the
distance of 35½ miles in 5½ hours. The total cost of the canal was
greatly in excess of the estimates, which placed it at eight million pounds,
as fifteen millions is the sum actually expended upon it. With such a vast
capital expenditure, it may be some time before the ordinary shareholders
can look for dividends, especially as there has not been any sudden rush
of traffic, such as many sanguine people expected. On the other hand,
traffic is continuously and steadily increasing, and there is reason to
believe that this great work will ultimately prove a commercial, as it has
an engineering, success.
271
Fig. 137c.—Sketch Map of The North Sea Canal.
Like several other canals for sea going ships this last addition to the
achievements of modern engineering is but the realisation of a project
conceived at a long past period. The idea of a canal to connect the
Baltic and the North Sea dates back into the Middle Ages, and indeed a
short canal was constructed in 1389, which by uniting two secondary
streams of the peninsula really did provide a waterway between the two
seas. The inefficiency of this means of communication may be inferred
from the fact of there having been proposed since that period no fewer
than sixteen schemes of canalisation between these two seas, of which
the recently completed North Sea Canal is the sixteenth, and it need
hardly be said the greatest, so that in comparison with it the rest vanish
into insignificance. The canal was commenced in 1887, and on the 20th
of June, 1895, it was opened by the reigning Emperor of Germany,
William II., with a very imposing naval pageant in which nearly a hundred
ships of war from the great navies of the world took part. A glance
at the accompanying sketch-map will show the great importance of this
canal as a highway of commerce. The entrance to the Baltic has hitherto
been round the peninsula of Denmark and through the narrow “belts”
and “sounds” that divide the Danish Islands, a course beset with imminent
perils to navigators, for the channels abound in rocks and dangerous
reefs, to say nothing about the frequent storms and the impediments of
ice floes. Yet as many as 35,000 vessels have lately had to take that
course annually, these representing a total tonnage of no less than
20,000,000 tons. The figures speak for the magnitude of the Baltic
shipping intercourse with the rest of the world; while the losses incurred
272in traversing these forbidding waters may be gathered from the statement
that since 1858, nearly 3000 ships have been wrecked in them, and a
greater number much damaged. Indeed, for large vessels, there is hardly
a more dangerous piece of navigation in all Europe. The importance
of this canal must not therefore be estimated solely by the saving of
length in ships’ course, though that is great, as the map shows.
The North Sea Canal is 61 miles long, 200 ft. wide at the surface, 85 ft.
wide at the bottom, and it will admit of vessels of 10,000 tons register
passing through, the average time of transit being about twelve hours.
The estimated cost of this undertaking was nearly eight and a quarter
million pounds sterling, and about one-third of this sum was contributed
by Germany, for whom the canal is of the greatest strategic importance
in case of war, for her fighting ships need not then traverse foreign waters.
The construction was therefore pushed forward with unusual energy, as
many as 8,600 men having been engaged on the works at one time. An
important naval station already exists at Kiel, the Baltic end of the
canal, where there is a splendid harbour. The engineer and designer of
this water-way is Herr Otto Baensch, who has devised much ingenious
machinery in connection with the immense tidal locks at the extremities
of the canal, and the swing bridges by which several lines of railway are
carried across it. In the construction of this canal there were no vast
engineering difficulties to be overcome, and hence striking feats of mountain
excavation or valley bridging are not to be met with in its course,
though in places there are some deep cuttings. The methods of excavating
and of steam dredging that were made use of have already been
illustrated in relation to the other works described in this article. The
country through which the canal passes does not present any unusually
picturesque features.
The several undertakings described in our chapter on Ship Canals are
now all completed and in active operation, and but for financial mis-management
and dishonest speculations, the same might probably have been
said of another great project, the name of which was on everyone’s lips a
short time ago, but in which public interest has lately waned; perhaps
from a mistaken impression that the construction itself is involved in a
common ruin with the fortunes of so many of its promoters, or that the
scheme was frustrated by some unforeseen and insurmountable engineering
difficulties. These assumptions have so little justification that it is
quite probable that Lesseps’ last great project may yet be completed
under more favourable auspices, and the Panama Canal unite the Atlantic
and Pacific Oceans. The Panama Canal Company still exists, and
possesses not only a very large part of the work almost quite finished, but
273all the extensive plant in perfect condition for resuming operations. The
original scheme provided for a tidal water-way between the two oceans,
without the intervention of a single lock. The canal was to be nearly 47
miles in length, 100 feet wide at the surface of the water, 72 feet wide at
the bottom, and 29 feet deep. The entrances are at Colon on the Atlantic
side, and at Panama on the Pacific. The latter is the eastern extremity,
and the western one is on the Atlantic side, owing to the configuration of
the isthmus which curves round the Panama Gulf that opens to the south.
A railway crosses the isthmus between the points already named, and the
route of the canal is laid down almost parallel with this railway, from
which it is nowhere far distant. For the first 20 miles from the Atlantic
side the land is only at a very moderate elevation above the sea-level, say
25 or 30 feet, but the next 11 miles is more hilly, the elevations reaching
at some points 150 to 170 feet, but these are only for short distances. A
few miles farther on, they rise still higher, until at Culebra the highest
point is met with, about 323 feet above the sea-level, and a cut of this
depth, 1,000 feet long, would be required. Through this highest part it
has been proposed to drive a tunnel, but the total extent of the deep
cutting at this part of the canal would be nearly 2 miles in length. This
would no doubt be a work of the most formidable magnitude, for it has
been calculated that no less than 24,000,000 cubic yards of material, consisting
for the most part of solid rock, would have to be removed. It is
not supposed, however, to offer any great difficulty in an engineering
point of view. Doubtless it would be costly, and would take some time
to accomplish. Another heavy piece of work would consist in constructions
for controlling a mountain torrent called the Rio Chagres, through
the valley of which the canal passes. This stream is very variable in the
quantity of water it discharges, rising in the rainy season 45 feet above
its ordinary level, and sending down forty times as much water as it does
in the dry season.
Mr. Saabye, an American engineer, who examined unofficially the
works of the Panama Canal in 1894, considers that about one half of the
total excavation has already been done, and one half of the total length
of the canal almost finished, and remaining in comparatively good condition.
At both ends, including 15 miles on the Atlantic side, there is
water 18 to 24 feet deep. “Besides the work already done, the Canal
Company has on hand, distributed at both terminals, and at convenient
points along the canal route, an immense stock of machinery, tools,
dredges, barges, steamers, tug-boats, and materials for continued construction.
At Panama, La Boca, and Colon, as well as along the canal,
are numerous buildings—large and small—for offices, workshops, storehouses,
and warehouses, and for lodging and boarding the men who were
employed on the work. The finished work, as well as all the machinery,
tools, materials, buildings, etc., are well taken care of and looked after.
The Canal Company employs one hundred uniformed policemen, besides
numerous watchmen, machinists, and others, whose sole duty consists in
watching the canal and looking after needed repairs of plant and care of
materials. In fact, the work and the whole plant is in such a condition,
so far as I could ascertain, that renewed construction could be taken up
and carried to a finish at any time it is desired to do so, after the Company’s
finances will permit.”
An enormous amount of money has already been expended on the
Panama Canal, and much of it lavishly and unnecessarily. A reorganised
274company may probably be able to form such estimates of the probable
cost of completing the work under careful and efficient management, that
financial confidence in it maybe restored. The canal not only already
possesses the requisite plant, but the route has the special advantages of
assistance in transport from the railway everywhere at but a short
distance from it, and fine commodious harbours for its ocean mouths. If
it were finished as originally designed, vessels could pass through it with
one tide, say in about six hours. It is understood that before the Panama
enterprise is again proceeded with, the Company think that a sum of
about £25,000 should be expended in a complete survey and re-study of all
the conditions, and the results submitted to the most eminent engineers.
A rival scheme for carrying a ship canal across the isthmus that
divides the Atlantic and Pacific Oceans is that known as the Nicaragua
Canal, as the proposed route is to cross Lake Nicaragua, an extensive
sheet of water situated some 400 or 500 miles north-west of the Panama
Canal. The lake is 110 miles long and 45 miles broad, and is on its
western side separated from the Pacific by a strip of land only 12 miles
wide, having at one point an elevation not exceeding 154 feet, which is
probably the lowest on the isthmus. The lake drains into the Caribbean
Sea on the east, by the San Juan river, a fine wide stream, 120 miles in
length, which is navigable for river boats from the Caribbean Sea up to
the lake, except near its upper part, where some rapids at certain times
prevent the passage of the boats. This canal project first took definite
form in 1850, when a survey was made and routes reported on. The
scheme attracted some attention in the United States, and in 1872, and
again in 1885, further surveys and estimates were made at the instance of
the States Government. The earlier schemes provided for the rise and
fall between sea and lake-–108 feet, a considerable number of locks—eleven
on each side, making the total length from sea to sea 181 miles.
The report of the latter advocated the canalization of the San Juan by a
very bold measure, namely, the construction of an immense dam, by
which the waters were to be retained in the valley for many miles at the
level of the lake. A company was formed to promote the project, and
again in 1890 there were more surveys and estimates made. This company
actually expended a considerable sum of money in attempting to
improve the harbour at Greytown, which would have formed the eastern
terminus, but had become silted up. But it was found afterwards that it
would be better to recommend the formation of an artificial harbour at
another point, by constructing two long piers running out into the sea,
although this change would involve the abandonment of a few hundred
yards of canal already excavated by the company near Greytown. The
company has also laid down about 12 miles of railway along the proposed
route, with wooden and iron sheds as workshops, offices, etc., and, moreover,
had dredges and other appliances at work. At this stage it was
proposed that the United States Government should guarantee the bonds
of the Nicaragua Canal Company to the extent of more than twenty
million pounds sterling. By an Act of Congress passed in March, 1895, a
commission of engineers was appointed for the purpose of ascertaining the
feasibility, permanence, and cost of construction and completion of the
Nicaragua Canal by the route contemplated. The report of this commission
is an elaborate and exhaustive review of the whole scheme based upon
a personal examination of the route, and on the plans, surveys, and estimates
made for the company, whose records, however, are stated in the
275report to be deficient in the supply of many important data. The Canal
Company’s project provided for the improvement of Greytown harbour,
as already stated, and from that place the canal was to proceed westward
at the sea-level to the range of high ground on the eastern side of
the isthmus, which elevation was to be ascended by three locks of unusual
depth, and a deep cut more than 3 miles in length, through rock to a
maximum depth of 324 feet. After passing this enormous cut, the route
provides for a series of deep basins, in which the water is confined by
numerous dams or embankments, the canal excavations being confined
to short sections through higher ground separating these basins. The
total length of these embankments will be about 6 miles, and their
heights will vary from a few feet to more than seventy. About 31 miles
from Greytown the canal reaches the San Juan river, which, however, by
means of an enormous dam across the valley at a place called Ochoa, 69
miles below the point at which it receives the waters of Lake Nicaragua,
is there practically converted into an arm of the lake. This dam, which
would raise the water of the river 60 feet above its present level, and would,
of course, flood the valley back to the lake, is the most notable feature of
the project. Its maximum height would be about 105 feet, and the weirs
on its crest, to discharge the surplus water, would require a total length of
nearly a quarter of a mile. Twenty-three smaller embankments would
also be needed for retaining the waters; the river would have to be
deepened in the upper part, and a channel dredged out in the soft mud of
the lake for 14 miles beyond the river. The big Ochoa dam is said to
have no precedent in engineering construction, on account of its great
height and the enormous volume of the waters it is intended to retain.
No doubt its construction and safe maintenance are within the range of
engineering skill, when a thoroughly exhaustive survey of the site has
been made, and the necessary funds are forthcoming. From the western
shore of the lake its level would also be extended by another great dam
crossing the valleys of the Tola and the Rio Grande, with a length of
2,000 feet and a height of 90 feet. The canal would then be carried to
the sea-level by a series of locks. The length of the canal from sea to
sea would be 170 miles, but of this only 40 miles of channel would require
to be excavated. The total cost of the work, as estimated by the
Nicaragua Canal Company, would be about fifteen million pounds sterling,
but the State Commission of Engineers thinks about double that amount
would be a safer calculation, and taking into account the imperfection of
the data, even this might be exceeded in certain contingencies. The
Government of the United States has been urged to expend a few
thousand pounds on another engineering commission, to make complete
surveys, and consider all the practical problems involved, including the
final selection of a route.
276
Fig. 138.—Britannia Bridge, Menai Straits.
IRON BRIDGES. — GIRDER BRIDGES. — SUSPENSION BRIDGES. — CANTILEVER BRIDGES. — THE TOWER BRIDGE, LONDON. — THE GREAT BROOKLYN BRIDGE.
The credit of having invented the arch is almost universally assigned
to the ancient Romans, though the period of its introduction and the
date of its first application to bridge building are unknown. That some
centuries before the Christian era, the timber bridges of Rome had not
been superseded by those of more permanent construction is implied in
the legend of the defence of the gate by Horatius Cocles—a tale which
has stirred the heart of many a schoolboy, and is known to everybody by
Macaulay’s spirited verses, in which
“Still is the story told,
How well Horatius kept the bridge,
In the brave days of old.”
Some of the arched bridges built by the Romans remain in use to this
day to attest the skill of their architects. The Ponte Molo at Rome, for
example, was erected 100 B.C.; and at various places in Italy and Spain
many of the ancient arches still exist, as at Narni, where an arch of 150 ft.
277span yet remains entire. Until the close of the last century the stone or
brick arch was the only mode of constructing substantial and permanent
bridges. And in the present century many fine bridges have been built
with stone arches. The London and Waterloo Bridges across the Thames
are well-known instances, each having several arches of wide span, attaining
in the respective cases 152 ft. and 120 ft. The widest arch in England,
and one probably unsurpassed anywhere in its magnificent stride of 200 ft.,
is the bridge across the Dee at Chester, built by Harrisson in 1820. At the
end of last century cast iron began to be used for the construction of
bridges, a notable example being the bridge over the Wear at Sunderland,
of which the span is 240 ft. But with the subsequent introduction of
wrought iron into bridge building a new era commenced, and some of the
great results obtained by the use of this material will be described in the
present article. In order that the reader may understand how the properties
of wrought iron have been taken advantage of in the construction
of bridges, a few words of explanation will be necessary regarding the
strains to which the materials of such structures are exposed.
Such strains may be first mentioned as act most directly on the materials
of any structure or machine, and these are two in number, namely, extension
and compression. When a rope is used to suspend a weight, the force
exerted by the latter tends to stretch the rope, and if the weight be made
sufficiently great, the rope will break by being pulled asunder. The weight
which just suffices to do this is the measure of the tenacity of the rope.
Again, when a brick supports a weight laid upon it, the force tends to compress
the parts of the brick or to push them closer together, and if the
force were great enough, the brick would yield to it by being crushed.
Now, a brick offers so great a resistance to a crushing pressure, that a
single ordinary red brick may be capable of supporting a weight of 18 tons,
or 40,320 lbs.—that is, about 1,000 lbs. on each square inch of its surface.
Thus the bricks at the base of a tall factory chimney are in no danger of
being crushed by the superincumbent weight, although that is often very
great. The tenacity of the brick, however, presents the greatest possible
contrast to its strength in resisting pressure, for it would give way to a pull
of only a few pounds. Cast iron resembles a brick to a certain extent in
opposing great resistance to being crushed compared to that which it offers
to being pulled asunder, while wrought iron far excels the cast metal in
tenacity, but is inferior to it in resistance to compression.
The following table expresses the forces in tons which must be applied
for each square inch in the section of the metals, in order that they may
be torn apart or crushed:
Tenacity per square inch, in tons.
Crushing pressure per square inch, in tons.
Cast iron
8
50
Wrought iron
30
17
Iron wire
40
...
Besides the direct strains which tend to simply elongate or compress the
materials of a structure or of a machine, there are modes of applying forces
which give rise to transverse strains, tending to twist or wrench the pieces
278or to bend them, or rupture them by causing one part of a solid to slide
away from the rest. Strains of this kind no doubt come into play in certain
subordinate parts of bridges of any kind; but if we divide bridges
according to the nature of the strains to which the essential parts of the
structure are subject, we may place in a class where the materials are
exposed to crushing forces only, all bridges formed with stone and brick
arches; and in a second class, where the material is subjected to extension
only, we can range all suspension bridges; while the third class is made
up of bridges in which the material has to resist both compression and extension.
This last includes all the various forms of girder bridges, whether
trussed, lattice, or tubular. The only remark that need be here made on
arched bridges is, that when cast iron was applied to the construction of
bridges, the chief strength of the material lying in its resistance to pressure,
the principle of construction adopted was mainly the same as that
which governs the formation of the arch; but as cast iron has also some
tenacity, this permitted certain modifications in the adjustment of the
equilibrium, which are quite out of the question in structures of brick and
stone.
Fig. 139.
Fig. 140.
Fig. 141.
Fig. 142.
The general principle of the construction of girder bridges is easily
explained by considering a simple case, which is almost within everybody’s
experience. Let us suppose we have a plank supported as in Fig. 139.
The plank will by its own weight sink down in the centre, becoming
curved in the manner shown; or if the curvature be not sufficiently obvious,
it may always be increased by placing weights on the centre, as at g. If
the length of the plank had been accurately measured when it was extended
flat upon the ground, it would have been found that the upper or concave
surface, a b, had become shorter, and the lower or convex surface, c d,
longer when the plank is supported only at the ends—a result sufficiently
obvious from the figure it assumes. It is plain, then, that the parts of the
wood near the upper surface are squeezed together, while near the lower
surface the wood is stretched out. Thus, the portions in the vicinity of the
upper and lower surfaces are in opposite conditions of strain; for in the
one the tenacity of the material comes into play, and in the other its power
of resisting compression. There is an intermediate layer of wood, however,
which, being neither extended or compressed, receives no strain. The
position of this is indicated by the line e f, called the neutral line. If the
plank, instead of being laid flat, is put upon its edge, as in Fig. 140, the
deflection caused by its weight will hardly be perceptible, and it will in
this position support a weight which in its former one would have broken
279it down. There is in this case a neutral line, e f, as before; but as the
part which is most compressed or extended is now situated at a greater
distance from the neutral line, the resistance of the material acts, as it
were, at a greater leverage. Again the portions near the neutral line are
under no strain; they do not, therefore, add to the strength, although they
increase the weight to be supported, and they may, for that reason, be removed
with advantage, leaving only sufficient wood to connect the upper
and lower portions rigidly together. The form of cast iron beams, Fig. 141,
which were used for many purposes, depends upon these principles. The
sectional area of the lower flange, which is subjected to tension, is six times
that of the upper one, which has to resist compression, because the strength
of cast iron to resist pressure is about six times greater than its power of
resisting a pull. If the upper flange were made thicker, the girder would
be weaker, because the increased weight would simply add to the tension
of the lower one, where, therefore, the girder would be more ready to give
280way than before. If we suppose the vertical web divided into separate
vertical portions, and disposed as at Fig. 142, the strength of the girder, and
the principle on which that strength depends, will be in no way changed,
and we at once obtain the box girder, which on a large scale, and arranged
so that the roadway passes through it, forms the tubular bridge. It is only
necessary that the upper part should have strength enough to resist the
compressing force, and the lower the extending force, to which the girder
may be subject; and wrought iron, properly arranged, is found to have the
requisite strength in both ways, without undue weight. The various forms
of trussed girders, the trellis and the lattice girders, now so much used for
railway bridges, all depend upon the same general principles, as does also
the Warren girder, in which the iron bars are joined so as to form a series
of triangles, as in Fig. 143.
Fig. 143.
Girders have been made of wrought iron up to 500 ft. in length, but the
cost of such very long girders is so great, that for spans of this width other
modes of construction are usually adopted.
Fig. 144.—Section of a Tube of the Britannia Bridge.
The Britannia Bridge, which carries the Chester and Holyhead Railway
across the Menai Straits, is perhaps the most celebrated example
of an iron bridge on the girder principle. It was designed by Stephenson,
but the late Sir W. Fairbairn contributed largely by his knowledge of iron
to the success of the undertaking, if he did not, in fact, propose the actual
form of the tubes. Stephenson fixed upon a site about a mile south of
Telford’s great suspension bridge, because there occurred at this point a
rock in the centre of the stream, well adapted for the foundation of a tower.
This rock, which rises 10 ft. above the low-water level, is covered at high
water to about the same depth. On this is built the central tower of the
bridge, 460 ft. from the shore on either side, where rises another tower, and
at a distance from each of these of 230 ft. is a continuous embankment of
stone, 176 ft. long. The towers and abutments are built with slightly sloping
sides, the base of the central or Britannia tower being 62 ft. by 52 ft., the
width at the level where the tubes pass through it, a height of 102 ft., being
reduced by the tapering form to 55 ft. The total height of the central
tower is 230 ft. from its rock foundation. The parapet walls of the abutments
are terminated with pedestals, the summits of which are decorated
by huge lions, looking landwards. As each line of rails has a separate
tube, there are four tubes 460 ft. long for the central spans, and four 230 ft.
long for the shorter spans at each end of the bridge. Each line of rails,
in fact, traverses a continuous tube 1,513 ft. in length, supported at intervals
281by the towers and abutments. The four longer tubes were built up on the
shore, and were floated on pontoons to their positions between the towers,
and raised to the required elevation by powerful hydraulic machinery. The
external height of each tube at the central tower is 30 ft., but the bottom
line forms a parabolic curve, and the other extremities of the tubes are
reduced to a height of 22¾ ft. The width outside is 14 ft. 8 in. Fig. 144
shows the construction of the tube, and it will be observed that the top and
bottom are cellular, each of the top cells, or tubes, being 1 ft. 9 in. wide, and
each of the bottom ones 2 ft. 4 in. The vertical framing of the tube consists
essentially of bars of ⟙-iron, which are bent at the top and bottom,
and run along the top and bottom cells for about 2 ft. The covering of the
tubes is formed of plates of wrought iron, rivetted to ⟙- and ∟-shaped ribs.
The thickness of the plates is varied in different parts from ½ in. to ¾ in.
The plates vary also in their length and width in the different parts of
the tubes, some being 6 ft. by 1¾ ft., and others 12 ft. by 2 ft. 4 in. The
joints are not made by overlapping the plates, but are all what are termed
butt joints, that is, the plates meet edge to edge, and along the juncture a
bar of ⟙-iron is rivetted on each side, thus: . The cells are also formed
282of iron plates, bolted together by ∟-shaped iron bars at the angles. The
rails rest on longitudinal timber sleepers, which are well secured by angle-iron
to the ⟙-ribs of the framing forming the lower cells. More than two
millions of rivets were used in the work, and all the holes for them, of
which there are seven millions, were punched by special machinery. The
rivets being inserted while red hot, and hammered up, the contraction
which took place as they cooled drew all the plates and ribs very firmly
together. In the construction of the tubes no less than 83 miles of angle-iron
were employed, and the number of separate bars and plates is said
to be about 186,000. The expansion and contraction which take place in
all materials by change of temperature had also to be provided for in the
mode of supporting the tubes themselves. This was accomplished by
causing the tubes, where they pass through the towers, to rest upon a series
of rollers, 6 in. in diameter, and these were arranged in sets of twenty-two,
one set being required for each side of each tube, so that in all thirty-two
sets were needed. There are other ingenious arrangements for the same
purpose at the ends of the tubes resting on the abutments, which are supported
on balls of gun-metal, 6 in. in diameter, so that they may be free to
move in any manner which the contractions and expansions of the huge
tubes may require. Each of the tubes, from end to end of the bridge,
contains 5,250 tons of iron. The mode in which these ponderous masses
were raised into their elevated position is described in the article on
“Hydraulic Power,” as it furnishes a very striking illustration of the utility
and convenience of that contrivance. The foundation-stone of the central
tower was laid in May, 1846, and the bridge was opened in October, 1850.
The tubes have some very curious acoustic properties: for example, the
sound of a pistol-shot is repeated about half a dozen times by the echoes,
and the tubular cells, which extend from one end of the bridge to the other,
were used by the workmen engaged in the erection as speaking-tubes. It
is said that a conversation may thus be carried on with a person at the
other end of the bridge, a distance of a quarter of a mile. The rigidity of
the great tubes is truly wonderful. A very heavy train, or the strongest
gale, produces deflections in the centre, vertical and horizontal respectively,
of less than one inch. But when ten or a dozen men are placed so that
they can press against the sides of the tube, they are able, by timing their
efforts so as to agree with the period of oscillation proper to the tube, to
cause it to swing through a distance of 1¼ in.—an illustration of facts of
great importance in mechanics, showing that even the most strongly built
iron structure has its own proper period of oscillation as much as the most
slender stretched wire, and that comparatively small impulses can, by
being isochronous with the period of oscillation, accumulate, as it were,
and produce powerful effects. Bridges are often tried by causing soldiers
to march over them, and such regulated movements form the severest test
of the freedom of the structures from dangerous oscillation. The main
tubes of the Britannia Bridge make sixty-seven vibrations per minute. The
expansion and contraction occurring each day show a range of from ½ in.
to 3 in. The total cost of the structure was £601,865.
A stupendous tubular bridge has also been built over the St. Lawrence
at Montreal, and the special difficulties which attended its construction
render it perhaps unsurpassed as a specimen of engineering skill. The
magnitude of the undertaking may be judged of from the following dimensions:
Total length of the Victoria Bridge, Montreal, 9,144 ft., or 1¾ miles;
length of tubes, 6,592 ft., or 1¼ miles: weight of iron in the tubes, 9,044
283tons; area of the surface of the ironwork, 32 acres; number of piers, 24,
with 25 spans between the piers, each from 242 ft. to 247 ft. wide.
Fig. 145.—Albert Bridge, Saltash.
Another singular modification of the girder principle occurs in the bridge
built by Brunel across a tidal river at Saltash, Fig. 145. Here only a single
line of rails is carried over the stream, which is, however, 900 ft. wide, and
is crossed by two spans of about 434 ft. wide. A pier is erected in the very
centre of the stream, in spite of the obstacles presented by the depth of the
water, here 70 ft., and by the fact that below this lay a stratum of mud
20 ft. in depth before a sound foundation could be reached. This work was
accomplished by sinking a huge wrought iron cylinder, 37 ft. in diameter
and 100 ft. in height, over the spot where the foundation was to be laid.
The cylinder descended by its own weight through the mud, and when the
water had been pumped out from its interior, the workmen proceeded to
clear away the mud and gravel, till the rock beneath was reached. On this
was then built, within the cylinder, a solid pillar of granite up to the high-water
level, and on it were placed four columns of iron 100 ft. high, each
weighing 150 tons. The two wide spans are crossed by girders of the kind
known as “bow-string” girders, each having a curved elliptical tube, the
ends of which are connected by a series of iron rods, forming a catenary
curve like that of a suspension bridge. To these chains, and also to the
curved tubes, the platform bearing the rails is suspended by vertical suspension
bars, and the whole is connected by struts and ties so nicely adjusted
as to distribute the strains produced by the load with the most beautiful
precision. When the bridge was tested, a train formed wholly of locomotives,
284placed upon the entire length of the span, produced a deflection in
the centre of 7 in. only. This bridge has sometimes been called a suspension
bridge because of the flexible chords which connect the ends of the
bows; but this circumstance does not in reality bring the bridge as a whole
under the suspension principle. The section of the bow-shaped tube is an
ellipse, of which the horizontal diameter is 16 ft. 10 in. and the vertical diameter
12 ft., and the rise in the centre about 30 ft. Beside the two fine spans
which overleap the river, the bridge is prolonged on each side by a number
of piers, on which rest ordinary girders, making its total length 2,240 ft., or
nearly half a mile; 2,700 tons of iron were used in the construction. As in
the case of the Britannia Bridge, the tubes were floated to the piers, and
then raised by hydraulic pressure to their position 150 ft. above the level
of the water. The bridge was opened by the late Prince Consort in 1860,
and has received the name of the Albert Bridge.
The general principle of the suspension bridge is exemplified in a chain
hanging between two fixed points on the same level. If two chains
were placed parallel to each other, a roadway for a bridge might be formed
by laying planks across the chains, but there would necessarily be a steep
descent to the centre and a steep ascent on the other side. And it would
be quite impossible by any amount of force to stretch the chains into a
straight line, for their weight would always produce a considerable deflection.
Indeed, even a short piece of thin cord cannot be stretched horizontally
into a perfectly straight line. It was, therefore, a happy thought
which occurred to some one, to hang a roadway from the chains, so that it
might be quite level, although they preserved the necessary curve. In
designing such bridges, the engineer considers the platform or roadway as
itself constituting part of the chain, and adjusts the loads in such a manner
that the whole shall be in equilibrium, so that if the platform were cut into
sections, the level of the road would not be impaired.
Public attention was first strongly drawn to suspension bridges by the
engineer Telford, who, in 1818, undertook to throw such a bridge across
the Menai Straits, and the work was actually commenced in the following
year. The Menai Straits Suspension Bridge has been so often described,
that it will be unnecessary to enter here into a lengthy account of it, especially
as space must be reserved for some description of other bridges of
greater spans. The total length of this bridge is 1,710 ft. The piers are
built of grey Anglesea marble, and rise 153 ft. above the high-water line.
The distance between their centres is 579 ft. 10½ in., and the centres of the
main chains which depend from them are 43 ft. below the line joining the
points of suspension. The roadway is 102 ft. above the high-water level,
and it has a breadth of 28 ft., divided into two carriage-ways separated by
a foot-track. The chains are formed of flat wrought iron bars, 9 ft. long,
3¼ in. broad, and 1 in. thick. In the main chains, of which there are sixteen,
no fewer than eighty such bars are found at any point of the cross
section, for each link is formed of five bars. These bars are joined by
cross-bolts 3 in. in diameter. The main chains are connected by eight
285transverse stays formed of cast iron tubes, through which pass wrought
iron bolts, and there are also diagonal ties joining the ends of the transverse
stays. The time occupied in the construction was 6½ years, and the
cost was £120,000. This bridge has always been regarded with interest
for being the first example of a bridge on the suspension principle carried
out on the large scale, and also for its great utility to the public, who, instead
of the hazardous passage over an often stormy strait, have now the
advantage of a safe and level roadway.
Fig. 146.—Clifton Suspension Bridge, near Bristol.
The Clifton Suspension Bridge over the Avon, near Bristol, is noted for
having a wider span than any other bridge in Great Britain, and it is remarkable
also for the great height of its roadway. The distance between
the centres of the piers—that is, the distance of the points between which
the chains are suspended—is more than 702 ft. Part of the ironwork
for this bridge was supplied from the materials of a suspension bridge
which formerly crossed the Thames at London, and was removed to make
room for the structure which now carries the railway over the river to the
Charing Cross terminus. Five hundred additional tons of ironwork were
used in the construction of the Clifton Bridge, which is not only much
longer than the old Hungerford Bridge, but has its platform of more than
double the width, viz., 31 ft. wide, instead of 14 ft. A view of this bridge
is given in Fig. 146, where its platform is seen stretching from one precipitous
bank of the rocky Avon to the other, and the river placidly flowing
more than 200 ft. below the roadway. The picturesque surroundings of
this elegant structure greatly enhance its appearance, and the view looking
south from the centre of the bridge itself is greatly admired, although the
286position may be at first a little trying to a spectator with weak nerves. The
work is also of great public convenience, as it affords the inhabitants of the
elevated grounds about Clifton a direct communication between Gloucestershire
and Somersetshire, thus avoiding the circuitous route through Bristol,
which was required before the completion of the bridge.
Fig. 147.
The use of iron wire instead of wrought bars has enabled engineers to
far exceed the spans of the bridges already described. The table on page
199 shows that iron wire has a tenacity nearly one-third greater than that
of iron bars, and this property has been taken advantage of in the suspension
bridge which M. Chaley has thrown over the valley at Fribourg, in Switzerland.
This bridge has a span of no less than 880 ft., and is constructed
entirely of iron wires scarcely more than ⅒ in. in
diameter. The main suspension cables, of which
there are two on each side, are formed of 1,056
threads of wire, and have a circular section of 5½
in. diameter. The length of each cable is 1,228 ft.,
and at intervals of 2 ft. the wires are firmly bound
together, so as to preserve its circular form. But
as the cable approaches the piers, the wires are
separated, and the two cables on each side unite
by the spreading out of the wires into one flat band
of parallel wire, which passes over the rollers at
the top of the piers, and is again divided into
eight smaller cables, which are securely moored to
the ground. Each of the mooring cables is 4 in.
in diameter, and is composed of 528 wires. In
order to obtain a secure attachment for the mooring
cables, shafts were sunk in the solid rock 52 ft.
deep, and the ingenious mode in which, by means
of inverted arches, an anchorage in the solid rock
is formed for the cables, will be understood by a
reference to Fig. 147. The cables pass downwards
through an opening made in each of the middle
stones, and are secured at the bottom by stirrup-irons
and keys. The suspension piers are built of
blocks of stone, very carefully shaped and put together
with cramps and ties, so as to constitute
most substantial structures. These piers are embellished
with columns and entablatures, forming
Doric porticoes, enclosing the entrances to the
bridge, which are archways 43 ft. high and 19 ft.
wide. The roadway is 21 ft. wide, and is supported on transverse beams,
5 ft. apart, upon which is laid longitudinal planking covered by transverse
planking. The roadway beams are suspended to the main cables by vertical
wire cables, 1 in. in diameter. The length of these suspension cables
of course varies according to their position, the shortest being ½ ft. and the
longest 54 ft. in length. Each suspension cable is secured by the doubling
back of the wires over a kind of stirrup, through which passes a plate of
iron, supported by the two suspension cables, the latter being close together,
and, indeed, only separated by the thickness of the suspension cables,
which hang between them. The roadway has a slight rise towards the
centre, its middle point being from 20 to 40 in. above the level of the ends,
according to the temperature.
287To test the stability of the bridge, fifteen heavy pieces of artillery, accompanied
by fifty horses and 300 people, were made to traverse it at various
speeds, and the results were entirely satisfactory. Indeed, a few years
afterwards the people of Fribourg had another wire bridge thrown over the
gorge of Gotteron, at about a mile from the former. This, though not so
long (640 ft.), spans the chasm at a great height, and in this respect is probably
not surpassed by any bridge in the world—certainly not by any the
length of which can compare with its own. The height of the roadway
above the valley is 317 ft., or about the same as that of the golden gallery
of St. Paul’s Cathedral above the street. The structure is very light, and
the sensation experienced when, looking vertically downwards through the
spaces between the flooring boards, you see the people below diminished
to the apparent size of flies, and actually feel yourself suspended in mid-air,
is very peculiar, as the writer can testify.
The Americans have, however, outspanned all the rest of the world in
their wire suspension bridges. They have thrown a suspension bridge of
800 ft. span over the Niagara at a height of 260 ft. above the water, to carry
not only a roadway for ordinary traffic, but a railway. Suspension bridges
are not well adapted for the latter purpose, but there seemed no other
solution of the problem possible under the circumstances. The bridge,
however, combines to a certain extent the girder with the suspension principle.
The girder which hangs from the main cables (for they are made of
wire), carries the railway, and below this is the suspended roadway for
passengers and ordinary carriages. The engineer of this work was Roebling,
who also designed many other suspension bridges in America.
The spans of any European bridges are far exceeded by that of the wire
suspension bridge which crosses the Ohio River at Cincinnati, with a
stride of more than 1,000 ft.; and this is, in its turn, surpassed by another
bridge which has been thrown over the Niagara. This bridge, which must
not be confounded with the one mentioned above, or with the Clifton
Bridge in England already described, merits a detailed description from
the audacity of its span, which is nearly a quarter of a mile, and entitles it
to the distinction of being the longest bridge in the world of one span.
Fig. 147a.—Clifton Suspension Bridge, Niagara.
The new suspension bridge at the Niagara Falls, called the Clifton
Bridge, of which a view is given in Fig. 147a, is intended for the use
of passengers and carriages visiting the Falls, and it is also the means of
more direct communication between several small towns near the banks of
the river. The bridge is situated a short distance below the Falls, crossing
the river at right angles to its course at a point where the rocks which
form the banks are about 1,200 ft. apart. The distance between the centres
of the towers is 1,268 ft. 4 in., and the bridge has by far the longest single
span of any bridge in the world, the distance between the points of suspension
being more than twice that of the Menai Bridge, and more than
six times the span of the widest stone bridge in England. This remarkable
suspension bridge was constructed by Mr. Samuel Keefer, and was
opened for traffic on the 1st of January, 1869, the actual time employed in
the work having been only twelve months. The cables and suspenders are
made of wire, which was drawn in England at Warrington and Manchester,
and the wires for the main cables were made of such a length, that each
wire passed from end to end of the cable without weld or splice. The length
of each of the two main cables is 1,888 ft., and of this length 1,286 ft. usually
hangs between the suspending towers, the centre being about 90 ft.
below the level of the points of suspension. This last distance, however,
289varies considerably with the temperature, for in winter the contraction produced
by the cold brings up the centre to 89 ft. below the level line, while
in summer it maybe 3 ft. lower. The centre of the bridge is about 190 ft.
above the water in summer, and 193 ft. in winter. The cables are each
formed of seven wire ropes, and each rope consists of seven strands, each
strand containing nineteen No. 9 Birmingham gauge wires of the diameter
of 0·155 in. The cables of this bridge do not hang in vertical planes, since
in the centre they are only 12 ft. apart; while at the towers, where they
pass over the suspension rollers, they are 42 ft. apart. The end of the platform
which rests on the right bank is 5 ft. higher than the other, and if a
straight line were drawn from one end to the other, the centre of the roadway
would be in winter 7 ft. above it, and in summer 4 ft. From each
point of suspension twelve wire ropes, called “stays,” pass directly to certain
points of the platform. The stays are not attached to the cables, but
pass over rollers on the tops of the towers, and are anchored in the rock,
independently of the cables. The longest stays are tangential to the curve
formed by the main cables, and they are fixed to the platform at a point
about half-way to the centre. Other stays proceed from the platform at
intervals of 25 ft., between the longest and the end of the bridge. The
thickness of the stays is varied according to the strain they have to bear,
and they form not only a great additional support to the platform, but they
also serve to stiffen the bridge and lessen the horizontal oscillations to
which the platform would be liable from the shifting loads it has to bear.
There are also stays which transversely connect the two cables. The wire
ropes by which the platform is suspended to the main cables are ⅝ths of an
inch in diameter, and have such a strength that the material would only yield
to a strain of 10 tons. These suspenders are placed 5 ft. apart and are 480
in number, the lengths, of course, being different according to the position.
To each pair of suspenders is attached a transverse beam, 13½ ft. long,
10 in. deep, and 2½ in. wide. Upon these beams—which are, of course,
5 ft. apart from centre to centre—rests the flooring, formed of two layers
of pine planking 1½ in. thick; and the roadway thus formed constitutes a
single track 10 ft. in width. Along each side of the platform is a truss the
whole length of the bridge, formed of an upper and a lower beam, 6½ ft.
apart, united by ties and diagonal pieces. The lower chord of the truss is
2 ft. below the road, and on it rolled iron bars are bolted continuously from
one end of the bridge to the other. The last arrangement contributes
greatly to stiffen the platform, vertically and horizontally. In the central
part of the bridge the flooring-boards are bolted up to the cables, and there
are studs formed of 2 in. iron tubes, so that the platform cannot be lifted
vertically without raising the cables also; and as thus 81 tons of the weight
of the cables vertically rest upon the platform, great steadiness is secured,
inasmuch as the central part of the cables must partake of any movement
of the platform, and their weight greatly increases the inertia to be overcome.
In order still further to prevent oscillations as much as possible, a
number of “guys” are attached to the bridge. These are wire ropes of the
same thickness as the suspenders, and they connect the platform with
various points of the bank—some going horizontally to the summit of the
cliffs, others vertically, but the majority obliquely. There are twenty-eight
guys on the side of the bridge next the falls, and twenty-six on the other
side. The thickness of the wire rope of which they are made being little
more than ½ in., they are scarcely visible, or rather appear like spider lines.
About 400 ft. of the length of the bridge in the centre is without either
290guys or stays except two small steel ropes, which, tightly strained from
cliff to cliff, cross each other nearly at right angles at the centre of the
bridge. The suspension towers are pyramidal in form and are built of
white pine, the timbers being a foot square in section and very solidly put
together, so that they are capable of bearing forty times the load which can
ever be put upon them. The towers are surmounted by strong frames of
cast iron, to which are fixed the rollers carrying the cables and stays to
their anchorage. The weight of the bridge itself, together with the greatest
load it can be required to bear, amounts to 363 tons. Its cost was £22,000,
and it was constructed without a single accident of any kind.
The foam of the great falls is carried by the stream beneath the bridge,
and in sunshine the spectator who places himself on the centre of its platform
sees in the spray driven by the wind, not a mere fragment of a rainbow,
or a semicircular arc, but the complete circle, half of which appears
beneath his feet. The gorge of the Niagara is very liable to furious blasts
of winds, for by its conformation it seems to gather the aërial currents into
a focus, so that a gentle breeze passing over the surrounding country is here
converted into a strong gale, sweeping down with great force between the
precipitous banks of the river. Indeed, one would suppose that the cavern
from which Æolus allows the winds to rush out, must be situated near
Niagara Falls. The bridge is not disturbed by ordinary winds, although
during its construction, before the stays and guys were fixed, it was subject
to considerable displacement from this cause. The peculiar arrangement
of the cables, by which they hang, not vertically, but widening out from the
centre of the bridge, giving what has been termed the “cradle” form, has
proved of the highest advantage, so that, with the aid of the guys and
stays, and the plan of attaching the central part of the roadway to the
cables, the bridge is believed to be capable of withstanding without damage
a gale having the force of 30 lbs. per square foot, although its total pressure
on the structure might then amount to more than 100 tons. The stability
of the structure was severely tested soon after its erection by a furious gale
from the south-west, by which the guys were severely strained; in fact, many
of them gave way. In one case an enormous block of stone, 32 tons in
weight, to which one of the guys was moored, was dragged up and moved
10 ft. nearer the bridge. This and some lateral distortion of the platform,
which was easily remedied, was all the damage sustained by the bridge. By
an increase of the strength of the guys, &c., and the addition of the two
diagonal steel wire ropes mentioned above, the bridge was soon made
stronger than before. Some years ago, when the Menai suspension bridge
was exposed to a storm of like severity, that structure suffered great
damage, the platform having been broken and some of it swept away. In
the great gale which swept down upon the Niagara bridge, although the
force of the wind was so great that passengers and carriages could not make
headway, the vertical oscillations of the bridge never exceeded 18 in., an
amount which must be considered extremely satisfactory in a bridge of the
kind, having a span of nearly a quarter of a mile.[4]
4. Notwithstanding the skill displayed in its construction, this bridge has, since the above
account was written, been destroyed by a tremendous hurricane.
291
Fig. 147b.—Living Model of the Cantilever Principle.
The great Forth Bridge, now (December, 1889) approaching completion,
is the first bridge on the cantilever and central girder principle
that has been erected in Great Britain, and it has also the distinction of
being by far the widest spanned bridge in all the world. We are told by
the engineers of the bridge that the cantilever and girder principle
is by no means new, for it has been adopted hundreds of years ago by
comparatively rude tribes in the construction of timber bridges, to which
it readily lends itself. Such bridges are described as having been erected
by the natives of Hindoostan, Canada, Thibet, etc., even at remote periods.
The principle of the cantilever and girder construction was well illustrated
by Mr. Baker, one of the engineers of the bridge, at a lecture given by
him at the Royal Institution, by means of what he termed “a living
model,” of which (Fig. 147b) shows the general arrangement. Two men,
seated on chairs, extend their arms and hold in their hands sticks, of
which the other ends butt against the chairs. The central girder is represented
by a shorter stick, suspended at a and b. We have here the
representation of two double cantilevers, the ropes at c and d, connected
with the weights, representing the anchorages of the landward arms of
the cantilevers. When a weight is placed on a b, which was done in the
“living model,” by a third man seating himself thereon, a tensile strain
comes into action in the ropes and in the men’s arms, while the sticks
abutting on the chairs have to resist a compressing force, and the weight
of the whole is borne by the legs of the chairs, also under compression.
Now let the reader imagine the men’s heads to be 360 feet above the
ground, and about a third of a mile apart, while the distance between a
and b is 350 feet, and he will have a rough but sufficiently clear idea, not
only of the principle upon which the Forth Bridge is constructed, but also
of the magnitude of one of its spans. To complete the comparison, Mr.
Baker further invited his hearers to suppose that the pull upon each arm
292of the men is equal to 10,000 tons, and that the legs of each chair press
on the ground with the weight of more than 100,000 tons.
The Forth Bridge spans the estuary at Queensferry nine miles north-west
from Edinburgh, and its purpose is to afford uninterrupted railway
communication along the eastern side of Scotland. It will, in effect,
shorten the railway journey between Edinburgh and Perth, or Aberdeen,
by nearly two hours. Queensferry had long been established as a usual
place for crossing the Forth, and readers of Scott’s “Antiquary” will
remember that the first chapter describes how Monkbarns and Lovel, by
some accidental delays to the coach, lost the tide, and had to wait, to sail
“with the tide of ebb and the evening breeze,” finding themselves, in the
meanwhile, pretty comfortable over a good dinner at the “Hawes Inn.”
This inn still stands, its situation being close to the southern end of the
great bridge. A design for the erection of a light suspension bridge at
the same spot was published at the beginning of the present century, but
although the spans were to be equal to those of the present bridge (17,000
feet), the different scale of the projects may be inferred from the total
weight of iron to be used being estimated at 200 tons, while 50,000 tons
will be required for the structure now approaching completion.
In 1873, an Act of Parliament was obtained authorizing the construction
of a suspension bridge at Queensferry, to carry the railway over the estuary.
The design comprised practically two bridges, each carrying a single line
of rails, the bridges being braced together at intervals. The central
towers were to have been 600 feet high, or about 100 feet loftier than any
other erection then existing in the world. The designer was the late Sir
Thomas Bouch, and preparations were made for carrying out the plans by
the erection of workshops and the manufacture of bricks for the piers.
But the project was knocked on the head by the terrible disaster at the
Tay Bridge, in December, 1879, when several of the central piers were
overturned by the force of the wind, with swift destruction to a passing
train, which was precipitated into the water, and every one of about ninety
persons in the train perished. Sir Thomas Bouch having been the
designer of the Tay Bridge, public confidence in his plan was shaken to
such an extent, that the four railway companies who were promoting the
construction of the suspension bridge abandoned the project in favour of
a design on the cantilever and central girder system, which was then
brought forward by Mr. (now Sir John) Fowler and Mr. Baker. When
the Bessemer process had made steel attainable at a cheap rate, these
engineers recognized the advantages which cantilever bridges, made of
that material, presented for the wide spans required for carrying railways
across navigable rivers, and in 1865 they had designed such a bridge, with
1,000 feet spans for a viaduct, across the Severn, near the position of the
present tunnel. It was not, however, until 1881 that the designs for the
Forth Bridge were published in English and American engineering
journals. These designs at once attracted attention, and scarcely a year
had elapsed before a railway bridge was built for the Canadian and Pacific
Railway, on the same principle, and this has been followed by others since.
It is, however, absurd to allege that the engineers took their ideas from
America, merely because these smaller undertakings have been completed
before the great work that dwarfs them all was open for traffic. The construction
of the Forth Bridge on its present design was commenced in
January, 1883. Its site at Queensferry is at a point where the estuary
narrows, and where, in the very middle of the channel, there is a small
293rocky island, called Inchgarvie, that furnishes a solid foundation for the
great central pier. On each side of this island the channels are about
one-third of a mile wide, and more than 200 feet deep, and through them
the tide rushes with great velocity. The impossibility of building up any
intermediate piers, under such circumstances, is sufficiently obvious—the
currents must be crossed at one span, if a railway bridge had to be made.
The formation of the piers for such a work presented many novel problems,
and much of the work had to be commenced in deep water; that is, the
ground of rock or hard clay had to be prepared, in some parts, as far as
90 feet below high water. Each pier stands on four caissons, which are
great tubes or drums of iron and steel, filled up with concrete. Each
weighed, when empty, about 400 tons, but when filled up with concrete,
the weight would be about 3,000 tons. The diameter of each is 70 feet,
and the deepest one is sunk 89 feet below the water, and it was with no
little labour that some of them were put in their places. Each caisson
has an outer and an inner tube, is 70 feet in diameter at the base, and 60
feet at the top. Seven feet from the bottom, an air-tight partition formed
a chamber in the lower part of the caisson, about 70 feet in diameter, by
7 feet high, and shafts sufficiently large to admit the passage of men and
tools led from the top. Air was forced into this chamber, when the caisson
had been sunk, expelling the water, and then men descended through the
shafts and locks, in which a high pressure of air was also maintained, and
excavated the material at the bottom, until the caisson had, by its own
weight, sunk to the depth required. The work in this air chamber was
carried on by means of electric lights, and ten or twelve weeks were occupied
in sinking each caisson. The pressure of the air in the working
chamber was sometimes as high as 35 pounds per square inch, or sufficient
to maintain the mercurial column in a barometer 72 inches high, instead
of the ordinary 29 or 30 inches. It was found that the labour in the
compressed air chamber could not be done by our home workmen, as
they were quite unaccustomed to the high air pressures required to keep
out the water; but arrangements were made for the assistance of a staff
of French workmen, inured to the conditions by long working under
water in the construction of the docks at Antwerp.
PLATE XIII.
THE FORTH BRIDGE.
The stores, offices and workshops, situated on a slight eminence near
the south end of the bridge, are very extensive, occupying, it is said, an
area of 50 acres. Here are great furnaces, cranes and machinery for
shaping and fitting the steel plates and bars ready for taking their
appointed places in the vast structure. An hydraulic crane may, for instance,
be seen lifting a ton weight flat steel plate that has been heated to redness
in a regenerative gas furnace, and transferring it to an hydraulic press, where
it is quickly and quietly bent to the required shape. The plate is then
cooled, and, when the edges have been planed, it is placed in position
with the adjoining plates, and the rivet holes are drilled by an ingenious
machine, specially designed by Mr. Arrol, the contractor, for that purpose.
It works upon 8–feet lengths of the tubes, and simultaneously cuts ten
rivet holes at different points in the circumference. All the different parts
of the structure are temporarily fitted together to ascertain that every
piece is properly adjusted. They are then marked according to the position
they are to take, and are laid aside until they are wanted. Thus the
work at the bridge has proceeded without any awkward hitches arising
from ill adjusted sections being brought together. At times, 1,800 tons of
finished steel-work has been turned out of these shops in a month, and
294this material, which was supplied by the Steel Company of Scotland, has
been found thoroughly trustworthy in every respect. Its strength is one-half
greater than that of the best wrought-iron, and the plates have
thrice the ductility of iron plates. The steel plates for the great tubes are
supplied in lengths of 16 feet, and of different thicknesses, between ⅜ths
of an inch and 1¼ inch.
Fig. 147c.—Principal Dimensions of the Forth Bridge.
The sketch, Fig. 147c, shows the general dimensions of the bridge proper,
or that part of the viaduct which will actually span the estuary. Of the three
great piers that support the cantilevers, it will be observed that the
central one, which rests on Inchgarvie, is wider than the other two. Each
consists mainly of four tubes, 12 feet in diameter, made of plates of steel
1¼ inch in thickness, and these rise to the highest part of the bridge,
which is 361 feet above the water, so that the structure is as lofty as St.
Paul’s Cathedral. These great tubes are not placed vertically, but
incline inwards towards the top, so that while the “straddle legs” of each
pair are 120 feet apart at the base, they are only 33 feet apart at the top.
These lofty columns are also braced together diagonally by other steel
tubes—that is, a tube passes from the foot of every column to each of
the other three. At the base of each column, the lowest spanning member
springs also (which appears like an arch, but is not so), as a tube of
12 feet diameter. Thus abutting or resting on enormously thick plates of
steel that cap the masonry of each pier, are five tubular steel limbs, three
of which are 12 feet in diameter, and two are 8 feet, and, besides these
five, girder members diverge from nearly the same centre. One of the
large tubular members is the first strut that rises obliquely to support the
upper structure. From the point where this strut meets the upper member,
a stay passes downwards with an opposite inclination to the lower
member, from its point of junction with which another strut rises, and so
on. All the struts, as being subject to compressing force, are made of
steel tubes; the straight upper members and the stays are lattice braced
girders of rectangular section. The apparent curve of the lower member—for
it is really made up of sections of straight tubes—may suggest the
notion of an arch; but the reader must remember that the principle of
this bridge has no relation to that of the arch. The cantilevers do not
unite the long arms they stretch, but each is an independent structure
with its own perfect stability, and it will not be clutched on or locked up to
its neighbours by the central girders. The weight of one of these 1,700 feet
spans is about 16,000 tons, and the heaviest train loads might be two
coal trains, weighing together, say 800 tons, or only one-twentieth of the
295dead weight of the structure. But, what would not generally be supposed,
the pressure of the wind is an element of much more importance in
considering the stability of the bridge than the weight of the rolling load.
It is to resist the wind pressure that the lofty columns that are only 33 feet
apart at the top across the bridge, plant their bases 120 feet asunder. The
estimated lateral pressure of the wind on one of the cantilevers, assuming
it as equal to 56 lbs. per square foot, would amount to 2,000 tons. These
strains are so fully provided for that the engineers are confident that a
hurricane of such a force as would desolate the country would leave the
Forth Bridge intact, even if the wind blew in opposite directions on the
two arms of the cantilever. To rend asunder the top ties, a pull equivalent
to the weight of 45,000 tons would be required, whilst the utmost
strain that passing trains could possibly bring upon these ties would be
less than 2,000 tons. A striking illustration of the strength of these huge
brackets was lately given by Mr. Baker himself, when in a public lecture
he assured his audience that half a dozen of our ponderous modern ironclads
might be hung from the cantilevers. Everyone knows that a
bracket requires to be strongest nearest the base, and the lower steel
arms that stretch out 680 feet each diminish in diameter until at the end
it has decreased to five feet, and the pairs approach each until, from
being 120 feet apart at the base, they are only 33 feet apart at the ends.
The central girders will each weigh about 1,000 tons, and only one end
of each will be attached to a cantilever, the other ends will simply rest
on what are called “rocking columns,” so that there may be freedom of
motion to allow play for the changes of position that will be induced by
changes of temperature expanding or contracting the huge masses of
metal.
The reader can hardly have failed to observe that the chief element
in the stability of the structure depends upon balancing a great mass of
metal on the one side of a pier by an equal mass on the other side. But
while each end of the central cantilever bears half the weight of a central
girder, the two shoreward cantilevers have this load at their inner ends
only. How is their balance maintained? In this way: the shoreward
arms are made about 10 feet longer than those that stretch over the
water and their extremities are also loaded with about 1,000 tons of iron,
built up within the shore piers.
The lofty columns of the piers were erected without any external
staging, from a temporary platform surrounding the piers and supporting
the necessary machinery. The weight of this platform with the machinery
on it was about 400 tons, and as the work proceeded it was raised as required
by hydraulic machines placed within the vertical columns. As the
height of these increased, the men and materials had to be conveyed to
the platform by cages moving between guide ropes and worked by steam
engines. From this platform were constructed not only the main columns,
but the great diagonal tubes, the bracing girders, and the viaduct girder.
The cantilevers were also put together without scaffolding. When the
first few feet of the lower member had been built out from the base, a
movable platform was hung round it, and on this platform were the
cranes for putting the plates into position, the furnace for heating the
rivets, and the hydraulic riveter of specially designed construction, without
noise or hammering, the riveting being completed by the application of a
pressure equal to 3 tons per square inch. The building up of the cantilever
arms on either side of each pier always proceeded at the same rate,
296so that the balance was constantly maintained. This building out from
each side of the pier, without the necessity of relying upon any temporary
scaffolding from below, is one great advantage of the cantilever system,
as it is both easier and safer than a system which relies upon the
temporary scaffolding raised from below. The Forth is for the time the
longest spanned bridge in the world; but it may not retain that honour
long, for the legislature of the United States has already authorized the
construction of a cantilever bridge, the spans of which are to be 2,480
feet. Still more gigantic is the project lately put forward by some competent
French engineers of bridging the English Channel from Folkestone
to Cape Grisnez in 70 spans on the cantilever system. The designs have
been completed and the calculations made, and no one doubts of the
engineering practicability of the scheme. But the cost is estimated at
about 34 million pounds sterling, or nearly six times as much as that
required for constructing the proposed Channel Tunnel; so that the scale
could be turned in favour of the bridge only if the political reasons that
were opposed to the tunnel were held not to be applicable to the bridge.
But it is difficult to conceive that the existing traffic could ever be
developed to such an extent as to make an undertaking of this magnitude
a commercial success.
Since the above account was written, the Forth Bridge was formally
opened on the 4th March, 1890, by the Prince of Wales, in the presence
of a great gathering of railway directors, eminent engineers, and other
distinguished persons from all parts. A very strong gale was blowing at
the time, and at this very hour the bridge was therefore subjected to
another severe but undesigned test of its stability. The perfect steadiness
and security of the structure impressed all who were present on that
occasion, and the train crossed the bridge, exposed to a wind pressure,
registered by the gauge, of 25 lbs. per square foot. At the luncheon following
the opening ceremony, the Prince announced that baronetcies had
been conferred upon Mr M. W. Thompson (the chairman of the Bridge
Company) and upon Sir John Fowler, and that Mr. Baker and Mr. Arrol,
the contractor for the works, were to be knighted. Sir John Fowler, the
engineer-in-chief, was born in 1817, and has been engaged in many other
important works of railway construction in Yorkshire, in that of the London
and Brighton Railway, in the Sheffield Waterworks, &c. The Metropolitan
Railway in London, which also was carried out by Sir John Fowler,
would alone suffice to make him famous as an engineer. Sir Benjamin
Baker is a much younger man, who has had a large and varied practice in
railway engineering in various parts of the world. He is in much request
on the American continent, and is now engaged in carrying out a ship
railway in Canada and a tunnel under the Hudson at New York. Sir
William Arrol began life at nine years of age as a “piecer” in a cotton
mill, but was afterwards apprenticed as an engineer. Subsequently he was
employed as a foreman by engineering firms in Glasgow. In 1866, he
began business on his own account at Dalmarnock, and obtained contracts
at first for smaller then for larger works connected with bridge and
viaduct building. He is distinguished for the energy and inventive
resources he displays in carrying out his undertakings.
297
A little more than four years after the opening of the Forth Bridge,
in June 1894, another great enterprise which had been commenced
eight years before, was inaugurated by the Prince and Princess of Wales
as representatives of Her Majesty the Queen. This was the Tower Bridge,
which not only is one of the most important public works of the century,
but one that presents features of interest and novelty that have never before
been combined in any single structure. The want of an adequate
communication between the shores of the Thames eastward of London
Bridge had long been felt, and was for years a subject of serious consideration
for the Metropolitan authorities. The congested state of the traffic
across London Bridge has often furnished a spectacle for the sight-seer,
and figures are not wanting to show that the number of foot-passengers
alone who daily traverse that bridge, which altogether is only 54 feet wide,
would be equal to the whole population of many considerable cities: for
in 1882 a count showed the daily average of pedestrians to be 110,525,
while the number of vehicles was 22,242. There was much difference of
opinion as to the best method of providing the required means of communication;
but there was an almost universal agreement as to its position
being selected just eastward of the Tower of London. The map of the
districts connected by the Tower Bridge which is given in Fig. 147d, will
show a reader who has any acquaintance with London the suitability of
the site. The problem of traversing the river at this point involved complex
conditions as affecting the vehicular traffic and the navigation, and
many different schemes were proposed and examined, comprised under
the three heads of bridges, tunnels and ferries. But a ferry is always an
imperfect means of communication, liable to accidents and interruptions
from fogs, and in severe weather from ice, rendering the transit impossible
for sometimes many days together. A tunnel beneath the river would, of
course, leave the navigation without impediment, but among its special
disadvantages are the great expense of construction and maintenance, for
it has been found that tunnels beneath waterways are very costly in both
respects. Besides, there would have to be long inclined approaches at
each end, and the cost would be enormously increased by the amount of
valuable land these would occupy. It was indeed proposed that the
tunnel should be provided instead with hydraulic lifts at each end, like
those often found in connection with the sub-ways at railway stations;
but such would have to be of Brobdignagian dimensions, and would
daily entail heavy expense. Then, as regards the bridges, schemes of
various kinds were proposed, some even bridging the whole 850 feet width
of the river at a single span, but all distinguishable by these important
characteristics: they either provided a high level roadway which requires
long inclines to reach it, but permitted lofty-masted ships to pass under
it; or, on the other hand, the roadway was to be made at a low level
with a clear headway above the water of moderate height. While avoiding
the inclined approaches, this plan would either prevent fully rigged
vessels passing to the wharves above the bridge, or some part of the
structure would have to open or swing aside, that the ships might pass
through the opening, thus completely interrupting the pedestrian and
298vehicular traffic for the time, with an amount of inconvenience that may
be imagined when, as often happens, twenty large ships or more might
pass in the course of a day, each causing a stoppage of five minutes in
the road traffic. Nor would it be without risks that large vessels could
pass through a comparatively narrow opening in a strong tide-way. Plans
for sub-ways, for high level roadways and for low level roadways, were
examined by Parliamentary Committees when powers to construct the
works were successively applied for by the Metropolitan authorities, and
much valuable evidence having been given, such objectionable features of
each scheme as have been already referred to were duly noted. At length
in 1878, Mr. Horace Jones, the late architect to the City of London, in a
report on the various projects, suggested the general plan on which the
present bridge is built, and this having been approved of by the Common
Council, steps were taken to obtain Parliamentary powers to raise the
necessary capital and to proceed with the works; but, for various reasons,
it was not until 1885 that the Act authorising the undertaking was passed.
In the meantime Mr. John Wolfe Barry was appointed engineer of the
structure, while Mr. Jones was to superintend the architectural details;
but after having received the honour of knighthood in 1885, he died in the
same year; and Mr. Barry, reconsidering the joint design, introduced
some new features and somewhat modified the architectural expression of
the structure. One striking point of originality about the Tower Bridge
is that while it is essentially an iron and steel construction as much as the
Forth Bridge, the heavy stiff metal-work is encased in masonry of elegant
and appropriate architectural design, by which the general desire that the
bridge should harmonize so far as might be, with the ancient historical
fortress it adjoins, has been happily realised. Then again, by the ingenious
engineering, the public have the advantage of a low level roadway,
while the largest vessels may pass freely through a wide space without
risk. These apparently incompatible advantages have been obtained
by the adoption of what is the bascule principle on a hitherto unattempted
scale. Bascule is a French engineering term, which is probably less
familiar to most of our readers than the thing itself. It is applied to the
platform of a draw-bridge which turns as the lid of a box does on its
hinges, to afford a passage over the stream or moat when it is horizontal,
and when drawn up vertically denies such passage. Smaller bascule
bridges on exactly the same plan as in the Tower Bridge may often be
seen in places having docks or canals, such as Hull, &c. In these a flap
or platform is let down from each side from the vertical position, in which the
water-way is open until the free edges meet together to form the roadway.
These platforms turn on horizontal pivots, and are counterpoised by loads
of stone or metal, so that they are without difficulty raised and lowered
by a winch or handle that turns a cogged pinion engaging the teeth of a
large quadrant.
PLATE XIV.
THE TOWER BRIDGE IN COURSE OF CONSTRUCTION.
“The Engineer” Swain Eng.
Fig. 147d.—Map of the Tower Bridge and its Approaches.
The following general description of the Tower Bridge is mainly abstracted
from a very full and excellent account of it drawn up in 1894 by
Mr. J. E. Tuit, engineer to Sir W. Arrol & Co., the contractors, in which
are embraced the whole of the technical details of the structure. The
map, Fig. 147d, shows the site of the bridge and its approaches, of which the
northern one begins close to the mint and passes along the east side of
the Tower of London to the northern abutment. This approach is formed
of a series of brick arches, and is nearly 1,000 feet long and 35 feet wide
in the roadway, with a footpath 12½ feet wide on either side of it. The
300incline is only a rise of 1 in 60, but the southern approach is slightly steeper,
namely, 1 in 40 leaving the street level at Tooley Street. At each abutment
there are also stairs connecting the banks of the river with the roadway
of the bridge. The width of the river between the two abutments is
880 feet, and this is divided, as shown in Fig. 147e, into two side spans,
each 270 feet wide, and one central span of 200 feet clear, making together
740 feet, the river piers, each of which is 70 feet wide, completing the
total span. The clear headway above high water, when the bascules or
leaves are down, is, in the middle span, 29½ feet in the centre, but only
15 feet at the ends; but when the leaves are raised for ships to pass, it is
about 143 feet. The headway at the shore sides of the piers is 27 feet,
but this is lessened to 23 feet and 20 feet at the north and south abutments
respectively. The roadway and footpaths are continued along the side
spans of the same width as on the approaches, but over the central span
the road is 32 feet, and each footway 8½ feet wide. The river piers are
said to be the largest in the world of the same kind, and their great area
was necessitated by the nature of the London clay on which they rest,
which was found incapable of bearing a load much exceeding four tons
per square foot without some risk of undue settlement.
The part of the piers below the bed of the river is formed of concrete,
while the upper part is brickwork, set in cement and faced with Cornish
granite. Upon each of the river piers rest four octagonal columns, built
up of flat steel plates, connected together at their edges by splayed angle-bars.
The columns are 120 feet high, and 5½ feet in diameter; those on
each pier are securely braced together, at certain stages also by plate
girders, 6 feet deep, to form a floor or landing, and the tops of the columns
are similarly joined together. At the height of 143 feet above high water
there are two footways, each 12 feet wide and 230 feet long, carried on girders
over the central span, and supported by the columns on each pier. It
must be noted that all the roadway, and, in fact, all the practical and useful
structure of the bridge, depend upon the steel-work alone, which is
supported mainly by the eight octagonal columns just mentioned. The
architectural features, which so appropriately clothe all the steel columns,
are added for æsthetic considerations, and their masonry takes no part in
bearing the weights and strains of the structure. Indeed, the stone-work
of the towers is carefully separated from the columns, which were covered
with canvas while the masonry was built round them, and spaces were
left at every point where compression of the steel-work would bring
weight upon the stone-work. This investment of the metal-work by
beautiful architecture is, as already mentioned, one of the most original
features of the Tower Bridge. The view of the work in progress, as given
in Plate VIII., which is one of the many beautiful illustrations in Mr. Tuit’s
book, will give the reader an opportunity of judging how much the structure
gains in sightliness by the addition of the architectural features.
Two hydraulic lifts are placed in each tower to convey pedestrians to and
from the higher level footways, when the moving parts of the bridge are
open, and stairs also are provided for the same purpose for those who
prefer them to using the lifts.
Fig. 147e.—The Tower Bridge.
Length of Bridge with its approaches
2680 feet.
Length of Northern approach
1000 feet.
Length of Southern approach
800 feet.
Width between N. and S. abutments
830 feet.
Width of central span
200 feet.
Width of side spans, each
270 feet.
Depth of River at high water under central span
33½ feet.
Depth of River at lowest tides under central span
12 feet.
Clear headway at high water when the leaves are down (varies from one part of the bridge to another)
20 to 29½ feet.
Clear headway in centre span at high water with the leaves raised
143 feet.
The side spans are really suspension bridges, but the chains have only
two links, connected at the lowest point by a pin 2½ feet in diameter, while
their higher ends are supported on the columns of the piers, and on
similar but shorter columns on the abutments. The horizontal pulls of
the chains on the piers are made to balance each other by connecting the
302chains to tie bars stretching across the central span, and the landward
ends of the chains, after passing over the lower columns of the abutments,
are securely anchored in enormous masses of concrete.
Each of the opening parts, or bascules, or leaves, as they may be called,
consists of four girders 18½ feet apart, rigidly braced together, and connected
at the pier end with a great shaft, 48 feet long and 1 foot 9 inches in
diameter, which turns in massive bearings, resting upon four fixed girders.
The leaf is counterbalanced on the shore side of the pivot shaft by 350
tons of lead and iron; the short leverage of the centre-weight and small
space available for it required the greater part of this weight to be of
lead, rather than of the less expensive metal. The pivot shaft passes
through the centre of gravity of the whole, so that, although the total
weight is nearly 1,200 tons, no very great power is required to set it in
motion, as the pivot shaft rests on rollers to diminish the friction. The
power for moving the leaf is applied to toothed quadrants of 42 feet radius,
of which two are fixed to the outside girders of each leaf, and are geared
into cogs moved by eight large hydraulic engines, with six accumulators,
into which water is pumped by two engines, each of 360 horse-power.
The total length of the bridge, including the approaches, is just half a
mile, and the height of the towers from the foundations is 293 feet, so that
if one of them were placed beside St. Paul’s Cathedral, it would compare
with it in height as shown in the sketch, Fig. 147f.
Fig. 147f.—Sketch.
303
The Clifton Bridge at Niagara Falls, which for a time had the distinction
of being the longest in span of any suspension bridge in the world,
has been fully described in previous pages; but more recently this bridge
has been surpassed in span, and in all other respects, by a structure that
immediately connects two of the most populous localities in the United
States of America. The Island of Manhattan, which is occupied by the
city of New York proper, has a population of nearly two millions, and a
strait on its eastern side, connecting Long Island Sound with New York
Harbour, alone divides it from the other great seats of population, called
respectively Long Island City and Brooklyn. This channel is about ten
miles long, and of a varying width, which may average three-quarters of
a mile. There are many ferries between the opposite shores, and the
waters are busy with steamers, sailing-boats, tugs, and craft of all kinds,
engaged either in traffic with ports near at hand, or in trade with distant
lands. At the southern end of this strait, near the point of its junction
with New York Bay, is the narrowest part of its course, and it is here that
it is crossed by the magnificent suspension bridge, known indifferently as
the East River Bridge, or Brooklyn Bridge, which provides land communication
between New York, with its population of two millions, and
Brooklyn, the fourth city of the States in point of size, with inhabitants
numbering about one million. Brooklyn is largely a residential place for
persons whose daily business is in New York. It has wide, well-planned
streets, many shaded by the luxuriant foliage of double rows of trees, and
possesses parks, public buildings, institutes, churches, etc., on a scale
commensurate with its importance.
The central span of Brooklyn Bridge, from tower to tower, is 1,595 feet,
and each shore part, extending from the tower to the anchorage of the
cables, is 930 feet span, while the two approaches beyond the anchorage
together add 2,534 feet to the total length, which is 5,989 feet, or considerably
over a mile. The centre span, it will be observed, is much
greater than that of the Niagara Falls Clifton Bridge, which was less than
one quarter of a mile, whereas the Brooklyn Bridge span extends to
something approaching one-third of a mile, or, more exactly, a few yards
longer than three-tenths. The width of the Brooklyn is another one of
its remarkable features, for this is no less than 85 feet, and includes two
roadways for ordinary vehicles, and two tramway tracks, on which the
carriages are moved by an endless cable, worked by a stationary engine
on the Brooklyn side. There is also a footpath, 13 feet wide, for
pedestrians. In this structure, as in many other suspension bridges,
advantage has been taken of the great tenacity of steel wire as compared
with iron bars. But here the wires are not twisted in strands like ropes,
but are laid straight together, and bound into a cylindrical form, each
wire being 3,572 feet long, and extending from end to end of the cables,
which are four in number, each calculated to bear a strain of 12,200 tons.
The number of wires in each cable is very great, for instead of about the
thousand of which the stranded wire cables usually consist, there are
5,296 steel wires wrapped closely round, and forming a cylinder 15¾
inches in diameter. Each wire is galvanised, that is, coated with zinc,
and then coated with oil. The towers over which the cables pass are of
304masonry, and rise to 272 feet above high-water; their dimensions at the
water level are 140 feet by 50 feet, which offsets diminish until at the top
they are 120 feet by 40 feet. At the anchor structures, the cables enter
the masonry at nearly 80 feet above high-water, and pass 28 feet into the
stonework for connection with the anchor chains. The anchorages are
masses of masonry, measuring at the base 129 feet by 119 feet, and at the
top 117 feet by 104 feet, with a height of 89 feet in front and 85 feet in the
rear. The weight of each anchor-plate is 23 tons. The roadway of the
bridge is suspended from the cables above the buildings and streets between
the towers and the anchorages. The approaches, on the Brooklyn
side 971 feet, on the New York side 1,563 feet, are carried on stonework
arches, which are utilised as warehouses, but where these approaches
cross streets, iron bridges are thrown over. The clear headway between
the centre of the roadway over the river at high-water is 135 feet, so that
there is no obstruction to navigation, and the headway at the towers is
119 feet, so that the roadway rises towards the centre about 3 feet 3 inches
in 100 feet. The two towers comprise more than 85,000 cubic yards of
masonry, and for various purposes 13,670 tons of concrete were used.
The work was commenced in January, 1870, and the first wire was
carried across on 29th May, 1877. The bridge was opened to the public
on the 24th of May, 1883, and the tramway four months later. The
bridge was made free for pedestrians in 1891, and in 1894 the tram-car
fares were reduced to five cents (2½d.) for two journeys. In that year,
41,927,122 passengers were carried on the cars. The average number of
persons daily crossing the bridge is estimated at about 115,000, although
on one day (11th Feb., 1895) as many as 225,645 passengers have been
carried on the cars. The cost of the work connected with this great
bridge was $15,000,000 (£3,125,000).
In relation to the subject of wide-spanning bridges, the erection has been
contemplated of structures which would surpass in magnitude and boldness
any of those yet named. Thus, in 1894, the New York Chamber of
Commerce proposed to throw across the River Hudson, which washes the
western side of New York, a bridge with a clear span of 3,200 feet (six-tenths
of a mile), and 500 feet clear height; and the project was declared
by an eminent and experienced engineer to be quite feasible.
PLATE XV.
THE BROOKLYN BRIDGE.
305
Fig. 148.—Newspaper Printing-Room, with Walter Machines.
A volume might be filled with descriptions of the machines which in
every department of industry have taken the place of slow and laborious
manual labour. But if even we selected only such machines as from
the beautiful mechanical principles involved in their action, or from their
effects in cheapening for everybody the necessaries and comforts of life,
might be considered of universal interest, the limits of the space we can
afford for this class of inventions would be far exceeded. The machines
for spinning, for weaving fabrics, for preparing articles of food, are in themselves
worthy of attention; then there is a little machine which in almost
every household has superseded one of the most primitive kinds of hand-work,
and that is the sewing machine. But all these we must pass over,
and confine our descriptions of special machines to a class in which the
interest is of a still more general and higher character, since their effect in
promoting the intellectual progress of mankind is universally acknowledged.
We need hardly say that we allude to Printing Presses, and if we add a
few lines on printing machines other than those which have given us cheap
literature, it is because these other machines also have contributed to the
general culture by giving us cheap decorative art, and in their general
principles they are so much akin to the former that but little additional
description is necessary.
306
The manner in which the youthful assistants of printers came to receive
their technical appellation of “devils” has been the subject of many
ingenious explanations. One of these is to the effect that the earlier productions
of the press, having imitated the manuscript characters, the uninitiated
supposed the impressions were produced by hand-copying, and in
consequence of their rapid production and exact conformity with each other,
it was thought that some diabolical agency must have been invoked. Another
story relates that one of Caxton’s first assistants was a negro boy, who
of course soon became identified in the popular mind with an imp from the
nether world. A very innocent explanation is put forward in another tale,
relating that one of the first English printers had in his employment a boy
of the name of De Ville, or Deville, which name was soon corrupted into
the now familiar title, and became the inheritance of this youth’s successors
in the craft. Perhaps a more probable and natural explanation might be
found in the personal appearance which the apprentices must have presented,
with hands, and no doubt faces also, smeared over with the black
ink which it was their duty to manipulate. For the ink was formerly always
laid upon large round pads or balls of leather, stuffed with wool. When
these balls, Fig. 149, which were, perhaps, about 12 in. in diameter, had
received a charge of ink, the apprentice dabbed the one against the other,
working them with a twisting motion, and after having obtained a uniform
distribution of the ink on their surfaces with many dexterous flourishes, he
applied them to the face of the types with both hands, until all the letters
were completely and evenly charged. The operation was very troublesome,
and much practice was required before the necessary skill was obtained,
while it was always a most difficult matter to keep the balls in good working
condition.
Fig. 149.—Inking Balls.
Fig. 150.—Inking Roller.
The first important step towards the possibility of a printing machine
was made, when for these inking balls was substituted a cylindrical roller,
mounted on handles, Fig. 150. The body of the roller is of wood, but it
is thickly coated with a composition which unites the qualities of elasticity,
softness, and readiness to take up the ink and distribute it evenly over the
types. The materials used for this composition are chiefly glue and treacle,
and sometimes also tar, isinglass, or other substances. Glycerine and
various other materials have also been proposed as suitable ingredients for
307these composition rollers, but it is doubtful whether the original compound
is not as efficacious as any yet tried. The composition is not unlike india-rubber
in its appearance and some of its properties. Fig. 150 represents
equally the mode in which the roller is applied to the type in hand presses,
and that in which it is charged with ink, by being moved backwards and
forwards over a smooth table upon which the ink has been spread.
From the time of the first appearance of printing presses in Europe down
to almost the beginning of the present century, a period of 350 years, no
improvement in the construction appears to have been attempted. They
were simply wooden presses with screws, on exactly the same plan as the
cheese-presses of the period. Earl Stanhope first, in 1798, made a press
entirely of iron, and he provided it with an excellent combination of levers,
so that the “platen,” or flat plate which overlies the paper and receives the
pressure, is forced down with great power just when the paper comes in contact
with the types. Such presses are capable of turning out about 250 impressions
per hour, and it should be noted that the very finest book printing
is still done by presses upon this principle. One reason is that in such cases,
where it is desired to print with the greatest clearness and depth of colour,
the ink employed is much thicker, or stiffer, and requires more thorough
distribution and application to the type than a machine can effect. Stanhope’s
press was not of a kind to meet the desire for rapid production, to
which the increasing importance of newspapers gave rise. The first practical
success in this direction was achieved by König, who, in 1814, set up
for Mr. Walter, the proprietor of the “Times,” two machines, by which that
newspaper was printed at the rate of 1,100 impressions per hour, the machinery
being driven by steam power.
The “Times” of the 28th November, 1814, in the following words made
its readers acquainted with the fact that they had in their hands for the
first time a newspaper printed by steam power:
“Our journal of this day presents to the public the practical result of the
greatest improvement connected with printing since the discovery of the
art itself. The reader of this paragraph now holds in his hand one of many
thousand impressions of ‘The Times’ newspaper, which were taken off by
a mechanical apparatus. A system of machinery almost organic has been
devised and arranged, which, while it relieves the human frame of its most
laborious efforts in printing, far exceeds all human powers in rapidity and
dispatch. That the magnitude of the invention may be justly appreciated
by its effects, we shall inform the public that after the letters are placed by
the compositors, and enclosed in what is called the ‘form,’ little more remains
for man to do than to attend upon and watch this unconscious agent
in its operations. The machine is then merely supplied with paper, itself
places the form, inks it, adjusts the paper to the form newly inked, stamps
the sheet, and gives it forth to the hands of the attendant, at the same time
withdrawing the form for a fresh coat of ink, which itself again distributes,
to meet the ensuing sheet now advancing for impression, and the whole of
these complicated acts is performed with such a velocity and simultaneousness
of movement that no less than 1,100 sheets are impressed in one hour.
That the completion of an invention of this kind, not the effect of chance,
but the result of mechanical combinations, methodically arranged in the
mind of the artist, should be attended with many obstructions and much
delay may be readily admitted. Our share in this event has, indeed, only
been the application of the discovery, under an agreement with the patentees,
to our own particular business; yet few can conceive, even with this limited
308interest, the various disappointments and deep anxiety to which we have
for a long course of time been subjected. Of the person who made the
discovery we have little to add. Sir Christopher Wren’s noblest monument
is to be found in the building which he erected: so is the best tribute of
praise which we are capable of offering to the inventor of the printing
machine comprised in the preceding description, which we have feebly
sketched, of the powers and utility of his invention. It must suffice to
say further, that he is a Saxon by birth, that his name is König, and that
the invention has been executed under the direction of his friend and countryman,
Bauer.”
Fig. 151.—Diagram of Cowper and Applegath’s Single Machine.
Each of the machines erected by König for the “Times” printed only
one side of the sheet, so that when they had been half printed by one
machine, they had then to be passed through the other, in order to be
“perfected,” as it is technically termed. These machines were greatly improved
by Messrs. Applegath and Cowper, who contrived also a modification
by which the sheets could be perfected in one and the same machine.
As the principle of these machines has been followed, with more or less
diversity of detail, in most of the printing machines at present in use, it is
very desirable to lay that principle clearly before the reader. The diagram,
Fig. 151, will make the action of Applegath and Cowper’s single-printing
machine easily understood. The type is set up on a flat form, A B, which
occupies part of the horizontal table, C D, the rest of which, A C, is the inking
table. E is a large cylinder, covered with woollen cloth, which forms the
“blanket.” The paper passes round this cylinder, and it is pressed against
the form. The small black circles, f, g, h, k, l, m, n, represent the rollers
for distributing the ink. f is called the ductor roller. This roller, which
revolves slowly, is made of metal, and parallel to it is a plate of metal,
having a perfectly straight edge, nearly, but not quite, touching the cylinder,
and at the other side, as well as at the extremities, bent upwards, so as to
form a kind of trough, to contain the ink, as a reservoir. The slow rotation
of the ductor conveys the ink to the next roller, which is covered with
composition, and being made to move backwards and forwards between
the ductor roller and the table at certain intervals, it is termed the vibrating
roller. The ink having thus reached the inking-table, is spread evenly
thereon by the distributing rollers, h, k, and it is taken up from the inking
table, as the latter passes under, by the inking rollers, l, m, n. The table,
C D, as a whole is constantly moving right and left in a horizontal direction,
309so that the form passes alternately under the impression cylinder, E, and
the inking rollers, l, m, n. The axles of the inking and distributing rollers
are made long and slender, and instead of turning in fixed bearings, they
rest in slots or notches, in order that, as the form passes below them, they
may be raised, so that they rest on the inking slab, and on the types, only
by their own weight. They are placed not quite at right angles to the direction
of the table, but a little diagonally. The sliding motion caused by this,
helps very much in the uniform spreading of the ink. By these arrangements
the form is evenly smeared with ink, since each inking roller passes
over it twice before it returns to meet the paper under E.
Fig. 152.—Diagram of Applegath and Cowper’s Perfecting Machine.
Fig. 153.—Cowper’s Double Cylinder Machine.
Fig. 152 is a similar diagram, to show the action of the double or perfecting
printing machine, in which the sheets are printed on both sides. It
will be observed that the general arrangement of impression cylinder,
rollers, &c., is represented in duplicate, but reversed in direction. There
are also two cylinders, B B, the purpose of which, as may be gathered from
an inspection of the diagram, is to reverse the sheets of paper, so that after
one side has been printed under the cylinder, E´, the blank surface may
be turned downward, ready to receive the impression from the form, A B.
Fig. 153 gives a view of the Cowper and Applegath double machine, as
actually constructed. The man standing up is called the feeder or layer-on.
He pushes the sheets forward, one by one, towards the tapes, which carry
them down the farther side of the more distant cylinder, under which they
pass, receiving the impression; and so on in the manner already indicated
310in the diagram, Fig. 152, until finally they reach a point where, released by
the separation of the two sets of tapes, they are received by the taker-off
(the boy who is represented seated on the stool), and are placed by him on
a table. The bed or table which carries the form moves alternately right
and left, impelled by a pinion acting in a rack beneath it, in such a manner
that the direction of the table’s motion is changed at the proper moment,
while the driving pulley continues to revolve always in the same direction.
The movements of the table and of the cylinders are performed in exact
harmony with each other, for these pieces are so connected by trains of
wheels and rack-work that the sheets of paper may always receive the impression
in the proper position as regards the margins, and therefore, when
the sheets are printed on both sides, the impressions will be exactly opposite
to each other. This gives what is technically called “true register,”
and as this cannot be secured unless the paper travels over both cylinders
at precisely the same rate, these are finished with great care by turning
their surfaces in a lathe to exactly the same diameter. The action of the
machine will not be fully understood without a glance at the arrangement
of the endless tapes which carry the paper on its journey. The course of
these may be followed in Fig. 154, and a simple inspection of the diagram
will render a tedious description unnecessary.
Fig. 154.—Tapes of Cowper’s Machine.
In Fig. 155 we have a representation of a steam-power printing machine,
such as is now very largely used for the ordinary printing of books, newspapers
of moderate circulation, hand-bills, &c., and in all the ordinary
work of the printing press. In this the table on which the form is placed
has a reciprocating motion, but the large cylinder moves continuously
always in the same direction. The feeder, or layer-on, places the sheet of
paper against certain stops, and at the right moment the sheet is nipped by
small steel fingers, and carried forwards to the cylinder, which brings it
into contact with the inked type. This is done with much accuracy of
register, for the impression cylinders gear in such a manner with the rest
of the parts that their revolutions are synchronous. This is a perfecting
machine, for the paper, after having received the impression on one side,
is carried by tapes round the other cylinder, where it receives the impression
on the other side, “set-off sheets” being passed through the press at
the same time. The axles of the impression cylinders are mounted at the
312ends of short rocking beams, by small oscillations of which the cylinders
are alternately brought down upon, or lifted off, the form passing below
them. A machine of this kind can print 900 impressions per hour, even of
good bookwork, and for newspaper or other printing, where less accuracy
and finish are required, it may be driven at such a rate as to produce 1,400
perfected impressions per hour.
Fig. 155.—Messrs. Hopkinson and Cope’s Perfecting Machine.
The machines used for lithographic printing by steam power are almost
identical in their general arrangement with that just described, which may
be taken as a representative specimen of the modern printing machine.
To such machines as those already described the world is indebted for
cheap books, cheap newspapers, and cheap literature in general. But when,
with railways and telegraphs, came the desire for the very latest intelligence,
the necessities of the newspaper press, as regards rapidity of printing,
soon required a greater speed than could possibly be attained by any
of the flat form presses; for in these the table, with the forms placed
upon it, is unavoidably of a considerable weight, and this heavy mass has
to be set in motion, stopped, moved in the opposite direction, and again
stopped during the printing of each sheet. The shocks and strains which
the machine receives in these alternate reversals of the direction of the
movement impose a limit beyond which the speed cannot be advantageously
increased. When Mr. Applegath was again applied to by the proprietors
of the “Times” to produce a machine capable of working off a still larger
number of impressions, he decided upon abandoning the plan of reciprocating
movement, and substituting a continuous rotary movement of the
type form. And he successfully overcame the difficulties of attaching
ordinary type to a cylindrical surface. The idea of placing the type on a
rotating cylinder is due to Nicholson, who long ago proposed to give the
types a wedge shape, so that the pieces of metal would, like the stones of
an arch, exactly fit round the cylindrical surface. The wedge-shaped types
were, however, so liable to be thrown from their places by the centrifugal
force, that Nicholson proposed also certain mechanical methods of locking
the types together after they had been placed on the circumference of the
drum. The plan he suggested for this purpose involved, however, such an
expenditure of time and trouble that his idea was never carried into practice.
Mr. Applegath used type of the ordinary kind, which was set up on flat
surfaces, forming the sides of a prism corresponding to the circumference
of his revolving type cylinder, which was very large and placed vertically.
The flat surfaces which received the type were the width of the columns of
the newspaper, and the type forms were firmly locked up by screwing down
wedge-shaped rules between the columns at the angles of the polygon.
These form the “column rules,” which make the upright lines between the
columns of the page, and by their shape they served to securely fix the type
in its place. The diameter of the cylinder to which the form was thus
attached was 5 ft. 6 in., but the type occupied only a portion of its circumference,
the remainder serving as an inking table. Round the great cylinder
eight impression rollers were placed, and to each impression roller was a
set of inking rollers. At each turn, therefore, of the great cylinder eight
sheets received the impression. These cylinders were, as already stated,
placed vertically, and, as it was necessary to supply the sheets from horizontal
tables, an ingenious arrangement of tapes and rollers was contrived,
by which each sheet was first carried down from the table into a vertical position,
with its plane directed towards the impression roller, in which position
it was stopped for an instant, then moved horizontally forwards round the
313impression cylinder, and was finally brought out, suspended vertically, ready
for a taker-off to place on his pile. This machine gave excellent results as
to speed and regularity. From 10,000 to 12,000 impressions could be
worked off in an hour, and the advantage was claimed for it of keeping
the type much cleaner, by reason of its vertical position. The power of
this machine may be judged of from one actual instance. It is stated that
of copies of the “Times” in which the death of the Duke of Wellington
was announced, 14th November, 1852, no less than 70,000 were printed in
one day, and the machines were not once stopped, either to wash the rollers
or to brush the forms. It may be mentioned, in order to give a better idea
of the magnitude of the operation of printing this one newspaper, that one
average day’s copies weigh about ten tons, and that the paper for the week’s
consumption fills a train of twenty waggons.
At the “Times” office and elsewhere, the vertical machine has some
years ago been superseded by others with horizontal cylinders. The fastest,
perhaps, of all these printing machines is that which is now known as the
“Walter Press,” so called either because its principle was suggested by
the proprietor of the “Times,” or merely out of compliment to him. The
improvements which are embodied in the Walter Press have been the
subject of several patents taken out in the names of Messrs. MacDonald
and Calverley, and it is to these improvements that we must now direct
the attention of the reader. But we must premise that such machines as
the Walter Press became possible only by the discovery of the means of
rapidly producing what is called a stereotype plate from a form of type.
A full account of the methods of effecting this is reserved for a subsequent
article, but here it may suffice to say, that when a thick layer of moist cardboard,
or rather a number of sheets of thin unsized paper pasted together
and still quite moist, is forced down upon the form by powerful pressure,
a sharp even mould of the type is obtained, every projection in the latter
producing a corresponding depression in the papier maché mould. When
the paper mould is dry, it may be used for forming a cast by pouring over
it some fusible metallic alloy, having the properties of becoming liquid at
a temperature which will not injure the mould, of taking the impressions
sharply, and of being sufficiently hard to bear printing from. One of the
improvements in connection with the Walter Press is in the mode of forming
cylindrical stereotype casts from the paper mould. For this purpose
the mould is placed on the internal surface of an iron semi-cylinder, with
the face which has received the impression of the type inwards. The central
part of the semi-cylinder is occupied by a cylindrical iron core, which
is adjusted so as to leave a uniform space between its convex surface and
the concave face of the mould. Into this space is poured the melted metal,
and its pressure forces the mould closely against the concave cylindrical
surface to which it is applied, so that the thickness becomes quite uniform.
The iron core has a number of grooves cut round it, and these produce in
the cast so many ribs, or projections, which encircle the inner surface, and
serve both to strengthen the cast and afford a ready means of obtaining
an exact adjustment. Not the complete cylinder, but only half its circumference,
is cast at once, the axis of the casting apparatus being placed
horizontally, and the liquid metal poured in one unbroken stream between
the core and the mould from a vessel as long as the cylinders. Fig. 156
is a section of the casting apparatus, in which a is the core, b the papier
maché mould, c the iron semi-cylinder containing it, d the metal which
has been poured in at the widened space, e. When the metal has solidified,
314the core is simply lifted off, and the cast is then taken out, in the form
of a semi-cylinder, the internal surface of which has exactly the diameter
of the external surface of the roller of the machine on which it is to be
placed, in company with another semi-cylindrical plate, so that the two
together encircle half the length of the roller, and when another pair of
semi-cylinders have been fixed on the other part of the roller, the whole
matter of one side of the newspaper sheet, usually four pages, is ready for
printing. One great advantage of working from stereotype casts made in
this way is that the form-bearing cylinder of the machine has no greater
circumference than suffices to afford space for the matter on one side of
the paper. The casts are securely fixed on the revolving cylinder by
elbows, which can be firmly screwed down. The casts are usually made
to contain one page each, so that four semi-cylinders, each half the length
of the revolving cylinder, are fixed on the circumference of the latter. The
process of casting in no way injures the paper mould, which is in fact generally
employed to produce several plates.
Fig. 156.
Fig. 157.—Diagram of the Walter Press.
The Walter Machine is not fed with separate sheets of paper, but takes
its supply from a huge roll, and itself cuts the paper into sheets after it has
impressed it on both sides. This is done by a very simple but effective
plan, which consists in passing the paper between two equal-sized rollers,
the circumference of which is precisely the length of the sheets to be cut.
These rollers grip the paper, but only on the marginal spaces; and on the
circumference of one of them, and parallel to its axis, is a slightly projecting
steel blade, which fits into a corresponding recess, or groove, in the
circumference of the other, and at this time the whole width of the sheet
is firmly held by a projecting piece acted on by a spring. Although the
Walter Machine, as actually constructed, presents to the uninitiated spectator
an apparently endless and intricate series of parallel cylinders and
rollers, yet it is in reality exceedingly simple in principle, as may be seen
by the diagram given in Fig. 157. In this we may first direct the reader’s
attention to the two cylinders, F1, F2, which bear the stereotype casts—one
of the matter belonging to one side of the sheet, the other of the matter
belonging to the other side, for the Walter Press is a perfecting machine—and
the web of paper having been printed by F1, against which it is pressed
by the roller, P1, passes straight, as shown by the dotted line, to the second
pair of cylinders, in order to be printed on the other side; and here, of
course, the form cylinder, F2, is below, and the impression cylinder, P2,
above, and an endless cleaning blanket is supplied to the latter to receive
315the set-off. The web of paper then passes between the cutting rollers, C, C1,
by which it is cut in sheets. But the knife has a narrow notch in the centre,
and one at each end, so that the paper is not severed at those parts, narrow
strips or tags being left, which maintain for a while a slight connection.
But the tapes, t1, t2, between which the paper is now carried, are driven at a
rather quicker rate than the web issues from C, C1; and the result is, that
the tags are torn, and the sheet becomes separated from the portion next
following it. Thus, as a separate sheet, it arrives at the horizontal tapes,
h, and is brought to another set of tapes mounted on the frame, r, rocking
about the centre, c, by which it is brought finally to the tapes, f1, f2,
which by the movement of r receive the sheets alternately. A sheet-flyer,
s, oscillates between the tapes, f1, f2; and as fast as the sheets arrive, lays
them down right and left alternately, and it only remains for the piles, p1, p2
so formed, to be removed. The inking apparatus of each form-cylinder
is indicated by the series of rollers marked I1, I2; and in this part of the
machine there are also some improvements over former presses, for the
distributing rollers are not made of composition, but of iron, turned with
great exactness to a true surface, and arranged so as not quite to touch
each other. At D is an apparatus for damping the paper, in which there
are hollow perforated cylinders, covered by blanket, and filled with some
porous material, which is kept constantly wet. These cylinders being made
to rotate rapidly, the centrifugal force causes the water to find its way uniformly
to the outside. Here the paper also passes between rollers intended
to flatten and to stretch it. At R is the great roll of paper, from which the
machine takes its supply. These rolls contain, perhaps, five miles length
of paper, and at first it was a matter of some difficulty to fix them firmly
on their wooden axles, so that they might be steadily unwound; but the
316contrivers of the Walter Press make these spindles as tight as may be required
by forming them in wedge-shaped pieces, which can be made to
increase the thickness of the spindle by drawing one upon another by
screws.
The great speed of the Walter Machine is secured by the paper being
drawn by the machine itself from a continuous web, instead of being laid on
in a separate sheet, so that the machine is not dependent on the dexterity
of the layers-on, who are besides necessarily highly-skilled workmen, and
therefore a great economy of wages results from using a machine which does
not require their services; and as the Walter Press also itself lays down
the perfected sheets, the necessary attendants are as few as possible. The
waste of paper and loss of time by stoppages are said to be extremely
small with this machine.
Fig. 148 will give some idea of the appearance of the printing-room
where one of the leading London daily papers is being printed by Walter
Presses.
Another fast printing machine is the type revolving cylinder machine
invented by Colonel Richard M. Hoe, and manufactured by the well-known
firm of Hoe and Company, New York, with whose name the history of fast
printing machines must ever be associated. In these machines the type is
placed on the circumference of a cylinder which rotates about a horizontal
axis, and the difficulties of securely locking up the type are successfully
overcome. The machines are made with two, four, six, eight, or ten impression
cylinders, and at each revolution of the great cylinder the corresponding
number of impressions are produced. The engraving on the
opposite page, Fig. 158, represents the two-cylinder machine, and an examination
of the figure will render its general action intelligible. The form
of type occupies about one-fourth of the circumference of the great cylinder,
the remainder being used as an ink-distributing surface. Round this main
cylinder, and parallel to it, are placed smaller impression cylinders, from
two to ten in number, according to the size of the machine. When the
press is in operation, the rotation of the main cylinder carries the type form
to each impression cylinder in succession, and it there impresses the paper,
which is made to arrive at the right time to secure true register. One person
is required for each impression cylinder, to supply the sheets of paper,
which have merely to be laid in a certain position, when, at the proper
moment, they are seized by the “grippers,” or fingers of the machine, and
after having been printed, are carried out by tapes, and laid in heaps by
self-acting sheet-flyers, by which the hands which are required to receive
and pile the sheets in other machines are dispensed with. The ink is contained
in a fountain placed beneath the main cylinder, and is conveyed
by means of rollers to the distributing surface of the main cylinder. This
surface, being lower than that of the type forms, passes by the impression
cylinders without touching them. For each impression cylinder there are
two inking rollers, receiving their supply of ink from the distributing surface
of the main cylinder. These inking rollers, the bearings of which are,
by springs, drawn towards the axis of the main cylinder, rise as the form
passes under them, and having inked it, they again drop on to the distributing
surface. Each page of the matter is locked up on a detachable segment
of the large cylinder, which segment constitutes its bed and chase.
The column-rules are parallel with the shaft of the cylinder, and are consequently
straight, while the head, advertising, and dark rules have the
form of segments of a circle. The column-rules are in the shape of a wedge,
318with the thin end directed towards the axis of the cylinder, so as to bind
the types securely. These wedge-shaped column-rules are held in their
place by tongues projecting at intervals along their length, and sliding in
grooves cut crosswise in the face of the bed. The spaces in the grooves
between the column-rules are accurately fitted with sliding blocks of metal
level with the surface of the bed, the ends of the blocks being cut away
underneath, to receive a projection on the sides of the tongues of the
column-rules. The locking up is effected by means of screws at the foot
of each page, by which the type is held as securely as in the ordinary
manner upon a flat bed. The main cylinder of the machine represented
in Fig. 158 has a diameter of 3 ft. 9 in., and its length is, according to the
size of the sheets to be printed, from 4 ft. 5 in. to 7 ft. 4 in. The whole is
about 20 ft. long, 10 ft. wide, including the platforms, and a height of 9 ft.
in the room in which it is placed suffices for its convenient working. The
steam power required is from one to two horse-power, according to the
length of the main cylinder. The speed of these machines is limited only
by the ability of the feeders to supply the sheets fast enough. The ten-cylinder
machine has, of course, ten impression cylinders, instead of two,
and there are ten feeding-tables, arranged one above the other, five on each
side. The main cylinder has a diameter of 4 ft. 9 in., and is 6 ft. 8 in. long.
The machine occupies altogether a space of 31 ft. by 16 ft., and its height is
18 ft. A steam engine of eight horse-power is sufficient to drive the ten-cylinder
machine, which is then capable of producing 25,000 impressions
per hour. The mechanism of the larger machines is precisely similar to
that of the two-cylinder machine, except such additional devices as are
necessary to carry the paper to and from the main cylinder at four, six,
eight, or ten points of its circumference. Much admirable contrivance is
displayed in the manner of disposing feeders as closely as possible round
the central cylinder.
Fig. 158.—Messrs. Hoe’s Type Revolving Cylinder Machine.
In some machines, such as Messrs. Hoe’s, Fig. 158, the sheet-flyers are
interesting features, for they form an efficient contrivance for laying down
and piling up, with the greatest regularity, sheet after sheet as it issues from
the press. The sheet-flyer is in fact an automatic taker-off, and therefore
it supersedes the services of the boy who would otherwise be required. It
is simply a light wooden framework of parallel bars, turning on one of its
sides as a centre; and the tapes carrying the sheet, passing down between
the bars, bring the paper down upon the frame, where its progress is then
stopped, the frame makes a rapid turn on its centre, lays down the sheet,
and quickly rises to receive another from the tapes. One can hardly see a
printing machine in action without being struck with the deftness with which
the sheet-flyer does its duty; for the precision with which it receives a sheet,
lays it down, and then quickly returns, to be ready for the next, suggest to
the mind of the spectator rather the movements of a conscious agent than
the motions of an unintelligent piece of mechanism. The sheet-flyer is seen
at the left-hand side of Fig. 158, where it is in the act of laying down a
sheet on the pile it has already formed.
Fig. 159.—Messrs. Hoe’s “Railway” Machine.
Fig. 160.—Napier’s Platen Machine.
The modern improvements in printing presses are well illustrated by
the machine represented on the opposite page, Fig. 159, which has been
designed by the Messrs. Hoe to work exclusively by hand. It is intended
for the newspaper and job work of a country office, and it works easily,
without noise or jar, by turning the handle always in the same direction,
producing 800 impressions in an hour. The bed moves backwards and
forwards on wheels running on rails, the reciprocating movement being
320derived from the circular one by means of a crank. From the mode in
which the table is carried backwards and forwards, the manufacturers call
this the “Railway Printing Machine.” The paper is fed to the underside
of the cylinder, which, after an impression has been given, remains stationary
while the bed is returning, and while the layer-on is adjusting his
sheet of paper. The axle of the impression cylinder carries a toothed
wheel working in a rack on the bed or table, the wheel having at two parts
of its circumference the teeth planed off so as to permit of the return of
the table without moving the impression cylinder, which is again thrown
into gear with the rack by a catch, so that the same tooth of the rack always
enters the same space on the toothed wheel, and thus a good register is
secured. The impression cylinder remains unaltered, whatever may be the
size of the type form, it being only necessary to place the forward edge of
the form always on the same line of the bed. Machines of a very similar
construction, but driven by steam power, are used in lithographic printing;
and in some of these machines advantage is elegantly taken of the fact
that, when a wheel rolls along, the uppermost point of its circumference is
always moving forward at exactly twice the velocity of its centre. Hence,
if the table of a printing machine rests on the circumference of wheels, a
backward and forward movement of the centres of these wheels, produced
by the throw of a crank through a space of 2 ft., would produce a rectilineal
reciprocating movement through a distance of 4 ft. of a table resting on the
circumference of the wheels. Any reader who is interested in geometry
or mechanics would do well to convince himself that the lowest point of
the wheel of a railway carriage, for example, is stationary (considered while
it is the lowest point), that the centre of the wheel is moving forwards with
the velocity of the train, and that the highest point of the wheel is moving
forwards with just twice the speed of the train. There is no difficulty about
the rate of rectilineal motion of the centre, but the reader cannot possibly
perceive the truth of the statement regarding the lowest and highest points
unless he reflects on the subject, or puts it to the test of experiment. Another
form of press which is used for good book printing is represented
321in the engraving, Fig. 160, which shows Napier’s platen machine. There
the action is similar to that of the ordinary hand presses as regards the
mode in which the paper is pressed against the face of the type; but the
movements are all performed by steam power, applied through the driving
belt, shown in the figure.
The various kinds of printing machines adapted to each description of
work are too numerous to admit of even a passing mention here; but those
which have been described may fairly be considered as representing the
leading principles of modern improvements. This article relates only to
the mechanism by which an impression is transferred from a form to the
surface of paper: the interesting and novel processes by which the form
itself may be produced—processes which have amazingly abridged the
printers’ labour and extended the resources of the art—deserve a separate
chapter, and will furnish matter for an article on Printing Processes, which
will be the better understood by being placed after chapters wherein the
scientific bases of some of these processes are discussed.
The machines used for printing patterns are, in principle, very similar
to those for letterpress printing; but the circumstance of several
different colours having frequently to go to the production of one pattern
leads to the multiplication, in the present class of machines, of the apparatus
for distributing the colours and impressing the materials. Pattern
printing machines are most extensively used for impressing fabrics, such
as calicoes, muslins, &c., and for producing the wall-papers for decorating
apartments. The machines employed for calicoes and for papers are so
much alike, that to describe the one is almost to describe the other.
The papers intended for paper-hangings are, in the first instance, covered
with a uniform layer of the colour which is to form the ground, and this is
done even in the case of papers which are to have a white ground. The
colours thus laid on, and those which are applied by the machine, are composed
of finely-ground colouring matters mixed with thin size or glue to a
suitable consistence, and the ground-tint is given by bringing the upper
surface of the paper, as it is mechanically unwound from a great roll, into
contact with an endless band of cloth emerging from a trough containing
a supply of the fluid colour. The paper then passes over a horizontal table,
where the layer of colour is uniformly distributed over its surface by brushes
moved by machinery, and the paper, after having been thoroughly dried,
is ready to receive the impressions. The impressions may be given by
flat blocks of wood on which the pattern is carved in relief, or from revolving
cylinders on which the pattern is similarly carved. The former is the
process of hand labour called “block printing,” and it requires much skill
and care on the part of the operator; but with these, excellent results are
obtained, as a correct adjustment of the positions of the parts of the pattern
can always be secured. The latter is the mode of printing mechanically
on rollers, corresponding with the type-bearing cylinders of the
322machines already described; but for pattern printing on paper they are
made of fine-grained wood, mounted on an iron axle, and they are carved
so that the design to be printed stands out in relief on their surface. One
of these rollers is represented in Fig. 161, and it should be clearly understood
that each colour in the pattern on a wall-paper requires a separate
roller, the design cut on which corresponds only with the forms the particular
colour contributes to the pattern. Such rollers being necessarily
somewhat expensive, as the pattern is usually repeated many times over
the cylindrical surface, the plan has been adopted of fastening a mass
of hard composition in an iron axle, and when this has been turned to a
truly cylindrical surface, it is made to receive plates of metal, formed of
a fusible alloy of lead, tin, and nickel. These plates are simply casts
from a single carved wooden mould of the pattern, which has thus only
once to be formed by hand. The plates are readily bent when warmed,
and are thus applied to the cylindrical surface, to which they are then
securely attached. It is found advantageous to cover the prominent parts
of the rollers which produce the impressions with a thin layer of felt, as
this substance takes up the colours much more readily than wood or metal,
and leaves a cleaner impression.
Fig. 161.—Roller for Printing Wall-Papers.
The machine by which wall-papers are printed is represented in Fig. 162,
where it will be observed that the impression cylinder has a very large
diameter, and that a portion of its circumference forms a toothed wheel,
which engages a number of equal-sized pinions placed at intervals about
its periphery. Each pinion being fixed on the axle of a pattern-bearing
roller, these are all made to revolve at the same rate. There is, however,
some adjustment necessary before that exact correspondence of the impressions
with each other is secured, which is shown on the printed pattern by
each colour being precisely in its appointed place. The rollers are constantly
supplied with colour by endless cloths, which receive it from the
troughs that are shown in the figure, one trough being appropriated to each
roller. Some of these machines can print as many as eighteen or twenty
different colours at once, by having that number of rollers; and it is easy
to see how, by dividing each trough into several vertical compartments, in
each of which a different colour is placed, it would be possible to triple or
even quadruple the number of colours printed by one machine.
The machinery by which calicoes are printed is almost identical in construction
with that just described, and presents the same general appearance.
There is, however, an important difference in the rollers, which in
calico printing are of copper or bronze, and have the design engraved upon
their polished cylindrical surface, not in relief, but in hollows. After the
whole surface of the roller becomes charged with colour, there is in the
machine a straight-edge, which removes the colour from the smooth surface,
323leaving only what has entered into the hollow spaces of the design,
which, as the roller comes round to the cloth, yield it up to the surface of
the latter. Thus, by a self-acting arrangement, the rollers are charged with
colour, cleaned, and made to give up their impressions to the stuff by parting
with the colour in the hollows. Rollers having patterns in relief are
also used in calico printing, the mechanism being then almost identical
with that of the former machine. It need hardly be said that great pains
are taken in the construction of such machines to have each part very
accurately adjusted, so that the impression may fall precisely upon the
proper place, without any blurring or confusion of the colours, and the
fact that an intricate design, having perhaps eighteen or twenty tints, can
be thus mechanically reproduced millions of times speaks volumes for the
accuracy and finish of the workmanship which are bestowed on such
printing machines.
Fig. 162.—Machine for Printing Paper-Hangings.
324
Fig. 163.—Chain-Testing Machine at Messrs. Brown and Lenox’s Works, Millwall.
HYDRAULIC POWER.
If a hollow sphere, a, Fig. 173, be pierced with a number of small holes at
various points, and a cylinder, b, provided with a piston, c, fitted into
it, when the apparatus is filled with water, and the piston is pushed inwards,
the water will spout out of all the orifices equally, and not exclusively from
that which is opposite to the piston and in the direction of its pressure.
The jets of water so produced would not, as a matter of fact, all pursue
straight paths radiating from the centre of the sphere, because gravity
would act upon them; and all, except those which issued vertically, would
take curved forms. But when proper allowance is made for this circumstance,
each jet is seen to be projected with equal force in the direction
of a radius of the sphere. This experiment proves that when pressure is
applied to any part of a liquid, that pressure is transmitted in all directions
equally. Thus the pressure of the piston—which, in the apparatus represented
in the figure, is applied in the direction of the axis of the cylinder
only—is carried throughout the whole mass of the liquid, and shows itself
by its effect in urging the water out of the orifices in the sphere in all directions;
and since the force with which the water rushes out is the same at
every jet, it is plain that the water must press equally against each unit of
area of the inside surface of the hollow sphere, without regard to the
position of the unit.
325If we suppose the piston to have an area of one square inch, and to be
pushed inwards with a force of 10 lbs., it cannot be doubted that the square
inch of the inner surface of sphere immediately opposite the cylinder will
receive also the pressure of 10 lbs.; and since the pressures throughout
the interior of the hollow globe are equal, every square inch of its area will
also be pressed outwards with a force equal to 10 lbs. Hence, if the total
area of the interior be 100 square inches, the whole pressure produced will
amount to a hundred times 10 lbs.
Fig. 164.—Pascal’s Principle.
Fig. 165.—Collar of Hydraulic Cylinder.
That water or any other liquid would behave in the manner just described
might be deduced from a property of liquids which is sufficiently obvious,
namely, the freedom with which their particles move or slide upon each
other. The equal transmission of pressure in all directions through liquids
was first clearly expressed by the celebrated Pascal, and it is therefore
known as “Pascal’s principle.” He said that “if a closed vessel filled with
water has two openings, one of which is a hundred times as large as the
other; and if each opening be provided with
an exactly-fitting piston, a man pushing in the
small piston could balance the efforts of a
hundred men pushing in the other, and he
could overcome the force of ninety-nine.”
Pascal’s principle—which is that of the hydraulic
press—may be illustrated by Fig. 164,
in which two tubes of unequal areas, a and
b, communicate with each, and are supposed
to be filled with a liquid—water, for example,
which will, of course, stand at the same level
in both branches. Let us now imagine that
pistons exactly fitting the tubes, and yet quite
free to move, are placed upon the columns of
liquid—the larger of which, b, we shall suppose
to have five times the diameter, and therefore
twenty-five times the sectional area, of the
smaller one. A pressure of 1 lb. applied to the
smaller piston would, in such a case, produce
an upward pressure on the larger piston of
25 lbs.; and in order to keep the piston at rest,
we should have to place a weight of 25 lbs. upon it. Here then a certain force
appears to produce a much larger one, and the extent to which the latter
may be increased is limited only by the means of increasing the area of
the piston. Practically, however, we should not by any such arrangement
be able to prove that there is exactly the same proportion between the
total pressures as between the areas, for the pistons could not be made to
fit with sufficient closeness without at the same time giving rise to so much
friction as to render exact comparisons impossible. We may, however,
still imagine a theoretical perfection in our apparatus, and see what further
consequences may be deduced, remembering always that the actual results
obtained in practice would differ from these only by reason of interfering
causes, which can be taken into account when required. We have supposed
hitherto that the pressures of the pistons exactly balance each other.
Now, so long as the system thus remains in equilibrium no work is done;
but if the smallest additional weight were placed upon either piston, that
one would descend and the other would be pushed up. As we have
supposed the apparatus to act without friction, so we shall also neglect the
326effects due to difference in the levels of the columns of liquid when the
pistons are moved; and further, in order to fix our ideas, let us imagine
the smaller tube to have a section of 1 square inch in area, and the larger
one of 25 square inches. Now, if the weight of the piston, a, be increased
by the smallest fraction of a grain, it will descend. When it has descended
a distance of 25 in., then 25 cubic inches of water must have passed into b,
and, to make room for this quantity of liquid, the piston with the weight of
25 lbs. upon it must have risen accordingly. But since the area of the larger
tube is 25 in., a rise of 1 in. will exactly suffice for this; so that a weight of
1 lb. descending through a space of 25 in., raises a weight of 25 lbs. through
a space of 1 in. This is an illustration of a principle holding good in all
machines, which is sometimes vaguely expressed by saying that what is
gained in power is lost in time. In this case we have the piston, b, moving
through the space of 1 in. in the same time that the piston a moves through
25 in.; and therefore the velocity of the latter is twenty-five times greater
than that of the former, but the time is the same. It would be more precise
to say, that what is gained in force is lost in space; or, that no machine,
whatever may be its nature or construction, is of itself capable of doing
work. The “mechanical powers,” as they are called, can do but the work
done upon them, and their use is only to change the relative amounts of
the two factors, the product of which measures the work, namely, space
and force. Pascal himself, in connection with the passage quoted above,
clearly points out that in the new mechanical power suggested by him in
the hydraulic press, “the same rule is met with as in the old ones—such
as the lever, wheel and axle, screw, &c.—which is, that the distance is increased
in proportion to the force; for it is evident that as one of the openings
is a hundred times larger than the other, if the man who pushes the
small piston drives it forward 1 in., he will drive backward the large piston
one-hundredth part of that length only.” Though the hydraulic press was
thus distinctly proposed as a machine
by Pascal, a certain difficulty prevented
the suggestion from becoming
of any practical utility. It was found
impossible, by any ordinary plan of
packing, to make the piston fit without
allowing the water to escape when the
pressure became considerable. This
difficulty was overcome by Bramah,
who, about the end of last century,
contrived a simple and elegant plan
of packing the piston, and first made
the hydraulic press an efficient and
useful machine. Fig. 166 is a view of
an ordinary hydraulic press, in which
a is a very strong iron cylinder, represented
in the figure with a part
broken off, in order to show that inside
of it is an iron piston or ram, b, which
works up and down through a water-tight
collar; and in this part is the invention
by which Bramah overcame
the difficulties that had previously been met with in making the hydraulic
press of practical use. Bramah’s contrivance is shown by the section of
327the cylinder, Fig. 165, where the interior of the neck is seen to have a groove
surrounding it, into which fits a ring of leather bent into a shape resembling
an inverted U. The ring is cut out of a flat piece of stout leather, well oiled
and bent into the required shape. The effect of the pressure of the water is
to force the leather more tightly against the ram, and as the pressure becomes
greater, the tighter is the fit of the collar, so that no water escapes
even with very great pressures. To the ram, b, Fig. 166, a strong iron table,
c, is attached, and on this are placed the articles to be compressed. Four
wrought iron columns, d d d d, support another strong plate, e, and maintain
it in a position to resist the upward pressure of the goods when the
ram rises, and they are squeezed between the two tables. The interior of
the large cylinder communicates by means of the pipe, f f, with the suction
and force-pump, g, in which a small plunger, o, works water-tight. Suppose
that the cylinders and tubes are quite filled with water, and that the ram
and piston are in the positions represented in the figure. When the piston
of the pump, g, is raised, the space below it is instantly filled with water,
which enters from the reservoir, h, through the valve, i, the valve k being
closed by the pressure above it, so that no water can find its way back
from the pipe, f, into the small cylinder. When the piston has completed
its ascent, the interior of the small cylinder is therefore completely filled
with water from the reservoir; and when the piston is pushed down, the
valve, i, instantly closes, and all egress of the liquid in that direction being
prevented, the greater pressure in g forces open the valve, k, and the water
flows along the tube, f, into the large cylinder. The pressure exerted by the
plunger in the small cylinder, being transmitted according to the principles
already explained, produces on each portion of the area of the large plunger
equal to that of the smaller an exactly equal pressure. In the smaller
328hydraulic presses the plunger of the forcing-pump is worked by a lever, as
represented in the figure at n; so that with a given amount of force applied
by the hand to the end of the lever, the pressure exerted by the press will
depend upon the proportion of the sectional area of b to that of o, and also
upon the proportion of the length m n, to the length m l. To fix our ideas,
let us suppose that the distance from m of the point n where the hand is
applied is ten times the distance m l, and that the sectional area of b is a
hundred times that of o. If a force of 60 lbs. be applied at n, this will produce
a downward pressure at m equal to 60 × 10, and then the pressure
transmitted to the ram of the great cylinder will be 60 × 10 × 100 = 60,000 lbs.
The apparatus is provided with a safety-valve at p, which is loaded with a
weight; so that when the pressure exceeds a desired amount, the valve
opens and the water escapes. There is also an arrangement at q for allowing
the water to flow out when it is desired to relieve the pressure, and the
water is then forced out by the large plunger, which slowly descends to
occupy its place. The body of the cylinder is placed beneath the floor in
such presses as that represented in Fig. 166, in order to afford ready access
to the table on which the articles to be compressed are placed.
Fig. 166.—Hydraulic Press.
The force which may, by a machine of this kind, be brought to bear upon
substances submitted to its action, is limited only by the power of the materials
of the press to resist the strains put upon them. If water be continually
forced into the cylinder of such a machine, then, whatever may be
the resistance offered to the ascent of the plunger, it must yield, or otherwise
some part of the machine itself must yield, either by rupture of the hydraulic
cylinder, or by the bursting of the connecting-pipe or the forcing-pump.
This result is certain, for the water refuses to be compressed, at least to any
noticeable degree, and therefore, by making the area of the plunger of the
force-pump sufficiently small, there is no limit to the pressure per square
inch which can be produced in the hydraulic cylinder; or, to speak more
correctly, the limit is reached only when the pressure in the hydraulic
cylinder is equal to the cohesive strength of the material (cast or wrought
iron) of which it is formed. It has been found that when the internal
pressure per square inch exceeds the cohesive or tensile strength of a rod
of the metal 1 in. square (see page 207), no increase in the thickness of the
metal will enable the cylinder to resist the pressure. Professor Rankine
has given the following formula for calculating the external radius, R, of a
hollow cylinder of which the internal radius is r, the pressure per square
inch which it is desired should be applied before the cylinder would yield
being indicated by p, while f represents the tensile strength of the
materials:
R = r√(f + p f – p)
We may see in this formula that as the value of p becomes more and more
nearly equal to f, the less does the divisor (f – p) become, and therefore
the greater is the corresponding value of R; and when f = p, or f – p = 0,
the interpretation would be that no value of R would be sufficiently great
to satisfy the equation. Thus a cylinder, made of cast iron, of which the
breaking strain is 8 tons per square inch, would have its inner surface ruptured
by that amount of internal pressure, and the water passing into the
fissures would exert its pressure with ever-increasing destructive effect.
With certain modifications in the proportions and arrangement of its
parts, the hydraulic press is used for squeezing the juices from vegetable
329substances, such as beetroots, &c., for pressing oils from seeds, and, in fact,
all purposes where a powerful, steady, and easily regulated pressure is
needed. Cannons and steam boilers are tested by hydraulic pressure, by
forcing water into them by means of a force-pump, just as it is forced into
the cylinder of the hydraulic press described above. This mode of testing
the strength has several great advantages; for not only can the pressure be
regulated and its amount accurately known; but in case the cannon or
steam boiler should give way, there is no danger, for it does not explode—the
metal is simply ruptured, and the moment this takes place, the water
flows out and the strain at once ceases.
The strength of bars, chains, cables, and anchors is also tested by hydraulic
power, and the engraving at the head of this article, Fig. 163, represents
the hydraulic testing machine at the works of Messrs. Brown and Lenox,
the eminent chain and anchor manufacturers, of Millwall. Immediately
in front of the spectator are the force-pumps, and the steam engine by
which they are driven. It will be observed that four plungers are attached
to an oscillating beam in such a manner that the water is continuously
forced into the hydraulic cylinder. The outer pair of plungers are of much
larger diameter than the inner pair, in order that the supply of water may
be cut off from the former when the pressure is approaching the desired
limit, and the smaller pair alone then go on pumping in the water, the pressure
being thus more gradually increased. Behind the engine and forcing
pump is the massive iron cylinder, where the pressure is made to act on
a piston, which is forced towards that end of the cylinder seen in the
drawing. The piston is attached to a very thick piston-rod, moving through
a water-tight collar at the other end of the cylinder. The effect of the
hydraulic pressure is, therefore, to draw the piston-rod into the cylinder,
and not, as in the apparatus represented in Fig. 166, to force a plunger out.
The head of the piston-rod is provided with a strong shackle, to which the
chains to be tested can be attached. In a line with the axis of the cylinder
is a trough, some 90 ft. long, to hold the chain, and at the farther end of
the trough is another very strong shackle, to which the other end of the
chain is made fast. A peculiarity of Messrs. Brown and Lenox’s machine
is the mode in which the tension is measured. In many cases it is deemed
sufficient to ascertain by some kind of gauge the pressure of the water in
the hydraulic cylinder, and from that to deduce the pull upon the chain;
but the Messrs. Brown have found that every form of gauge is liable to
give fallacious indications, from variations of temperature and other circumstances,
and they prefer to measure the strain directly. This is accomplished
by attaching the shackle at the farther extremity of the trough to
the short arm of a lever, turning upon hard steel bearings, the long arm of
this lever acting upon the short arm of another, and so on until the weight
of 1 lb. at the end of the last lever will balance a pull on the chain of
2,240 lbs., or 1 ton. The tension is thus directly measured by a system
of levers, exactly resembling those used in a common weighing machine,
and this is done so accurately that even when a chain is being subjected
to a strain of many tons, an additional pull, such as one can give to the
shackle-link with one hand, at once shows itself in the weighing-room.
The person who has charge of this part of the machine places on the end of
the lever a weight of as many pounds as the number of tons strain to which
the chain to be tested has to be submitted. The engineer sets the pump
in action, the water is rapidly forced into the cylinder, the piston is thrust
inwards, and the strain upon the chain begins; the engineer then cuts off
330the water supply from the larger force-pumps, and the smaller pair go on
until the strain becomes sufficient to raise the weight, and then the person
in the weighing-room, by pulling a wire, opens a valve in connection with
the hydraulic cylinder, which allows the water to escape, and the strain is
at once taken off. This testing machine, which is capable of testing cables
up to 200 tons or more, was originally designed by Sir T. Brown, the late
head of the firm, and not only was the first constructed in the country, but
remains unsurpassed in the precision of its indications.
The testing of cables, which we have just described, is a matter of the
highest importance, for the failure of cables and anchors places ships and
men’s life in great danger, since vessels have frequently to ride out a storm
at anchor, and should the cables give way, a ship would then be almost
entirely at the mercy of the winds and waves. Hence the Government have,
with regard to cables and anchors, very properly made certain stringent
regulations, which apply not only to the navy but to merchant shipping. The
chain-cable is itself a comparatively modern application of iron, for sixty
years ago our line-of-battle ships carried only huge hempen cables of some
8 in. or 9 in. diameter. Chain-cables have now almost entirely superseded
ropes, though some ships carry a hempen cable, for use under peculiar circumstances.
The largest chain-cables have links in which the iron has a
diameter of nearly 3 in., and these cables are considered good and sound
when they can bear a strain of 136 tons. Such are the cables used in the
British navy for the largest ships. Of course, there are many smaller-sized
cables also in use, and the strains to which these are subjected when they
are tested in the Government dockyards vary according to the thickness
of the iron; but it is found that nearly one out of every four cables supplied
to the Admiralty proves defective in some part, which has to be replaced
by a sounder piece. The chain-cables made by Messrs. Brown and
Lenox for the Great Eastern are, as might have been expected, of the
very stoutest construction; the best workmanship and the finest quality of
iron having been employed in their manufacture. These cables were tested
up to 148 tons, a greater strain than had ever before been applied as a test
to any chain, and it was found that a pull represented by at least 172 tons
was required to break them. It is difficult to believe that a teacup-full of
cold water shoved down a narrow pipe is able to rend asunder the massive
links which more than suffice to hold the huge ship securely to her anchors,
but such is nevertheless the sober fact. The regulations of the Board of
Trade require that every cable or anchor sold for use in merchant ships is
to be previously tested by an authorized and licensed tester, who, if he
finds it bears the proper strain, stamps upon it a certain mark.
The means which is afforded by hydraulic power of applying enormous
pressures has been taken advantage of in a great many of the arts, of which,
indeed, there are few that have not, directly or indirectly, benefited by this
mode of modifying force. An illustration, taken at random, may be found
in the machinery employed at Woolwich for making elongated rifle-bullets.
The bullets are formed by forcing into dies, which give the required shape,
little cylinders of solid lead, cut off by the machine itself from a continuous
cylindrical rod of the metal. The rod, or rather filament, of lead is wound
like a rope on large reels, from which it is fed to the machine. It is in the
production of this solid leaden rope or filament that hydraulic pressure is
used. About 4 cwt. of melted lead is poured into a very massive iron
cylinder, the inside of which has a diameter of 7½ in., while the external
diameter is no less than 2 ft. 6 in., so that the sides of the cylinder are
331actually 11¼ in. thick. When the lead has cooled so far as that it has
passed into a half solid state, a ram or plunger, accurately fitting the bore
of the cylinder, is forced down by hydraulic pressure upon the semi-fluid
metal. This plunger is provided with a round hole throughout its entire
length, and as it is urged against the half solidified metal with enormous
pressure, the lead yields, and is forced out through the hole in the plunger,
making its appearance at the top as a continuous cylindrical filament, quite
solid, but still hot. This is wound upon the large iron reels as fast as it
emerges from the opening in the plunger, and these reels are then taken to
the bullet-shaping machine, which snips off length after length of the leaden
cord, and fashions it into bullets for the Martini-Henry rifle. The leaden
pipes which are so much used for conveying water and gas in houses are
made in a similar manner, metal being forced out of an annular opening,
which is formed by putting an iron rod, having its diameter of the required
bore of the pipe, in the middle of the circular opening. The lead in escaping
between the rod and the sides of the opening takes the form of a pipe, and
is wound upon large iron reels, as in the former case.
Fig. 167.—Section of Hydraulic Lift Graving Dock.
Fig. 168.—Section of Column.
Another interesting application of hydraulic power is to the raising of
ships vertically out of the water, in order to examine the bottoms of their
hulls, and effect any necessary repairs. The hydraulic lift graving dock, in
which this is done, is the invention of Mr. E. Clark, who, under the direction
of Mr. Robert Stephenson, designed the machinery and superintended
332the raising of the tubes of the Britannia Bridge, where a weight of 1,800
tons was lifted by only three presses. The suitability of the hydraulic
press for such work as slowly raising a vessel was doubtless suggested to
him in connection with this circumstance, and the durability, economy, and
small loss of power which occurs in the action of the press, pointed it out
as particularly adapted for this purpose. The ordinary dry dock is simply an
excavation, lined with timber or masonry, from which the tide is excluded by
a gate, which, after the vessel has entered the dock at high water, is closed;
and when the tide has ebbed, and left the vessel dry, the sluice through
which the water has escaped is also closed. In a
tideless harbour the water has to be pumped out
of the dock, and this last method is also adopted
even in tidal waters, so that the docks may be
independent of the state of the tides. The lift of
Clark’s graving dock is a direct application of the
power of the hydraulic press, and we select for
description the graving dock constructed at the
Victoria Docks for the Thames Graving Dock
Company, whose works occupy 26 acres. Fig. 167
is a transverse section of this hydraulic lift graving
dock, in which there are two rows of cast iron
columns, 5 ft. in diameter at the base, where they
are sunk 12 ft. in the ground, and 4 ft. in diameter
above the ground. The clear distance between
the two rows is 60 ft., and the columns are placed
20 ft. apart from centre to centre, sixteen columns
in each row, thus giving a length of 310 ft. to the
platform, but vessels of 350 ft. in length may practically
be lifted. The bases of the columns, one
of which is represented in section in Fig. 168,
are filled with concrete, on which the feet of
the hydraulic cylinders rest. The outer columns
support no weight, but act merely as guides for
the crossheads attached to the plungers. The
height of the columns is 68½ ft., and a wrought
iron framed platform connects the columns at
the top. In order that any inequalities in the
height of the rams may be detected, a scale is
painted on each column, to mark the positions of
the crossheads. The hydraulic cylinders, which
are within these columns, have solid rams of
10 in. diameter, with a stroke of 25 ft., and on
the tops of these are fastened the crossheads,
7½ ft. long, made of wrought iron, and supporting
at the ends bars of iron, to the other ends of
which the girders of the platform are suspended.
The girders are, therefore, sixteen in number, and
together form a gridiron platform, which can be raised or lowered with the
vessel upon it. The thirty-two hydraulic cylinders were tested at a pressure
of more than 3 tons per square inch. The water is admitted immediately
beneath the collars at the top (this being the most accessible position) by
pipes of only ½ in. diameter, leading from the force-pumps, of which there
are twelve, of 1⅞ in. diameter, directly worked by a fifty horse-power steam
333engine. The presses are worked in three groups—one of sixteen, and two
of eight presses,—so arranged that their centres of action form a sort of
tripod support, and the presses of each group are so connected that perfect
uniformity of pressure is maintained. The raising of a vessel is accomplished
in about twenty-five minutes, by placing below the vessel a pontoon,
filled in the first instance with water, and then raising the pontoon
with the vessel on it, while the water is allowed to escape from the pontoon
through certain valves; then when the girders are again lowered, the pontoon,
with the vessel on it, remains afloat. Thus in thirty minutes a ship
drawing, say, 18 ft. of water is lifted on a shallow pontoon, drawing, perhaps,
only 5 ft., and the whole is floated to a shallow dock, where, surrounded
with workshops, the vessel, now high and dry, is ready to receive the necessary
repairs. The number of vessels which can thus be docked is limited
only by the number of pontoons, and thus the same lift serves to raise and
lower any number of ships, which are floated on and off its platform by
the pontoons. With a pressure in the hydraulic cylinders of about 2 tons
upon each square inch, the combined action of these thirty-two presses
would raise a ship weighing 5,000 tons.
Hydraulic power has been used not only for graving docks, as shown in
the above figures, but also for dragging ships out of the water up an inclined
plane. The machinery for this purpose was invented by Mr. Miller for
hauling ships up the inclined plane of “Martin’s slip,” at the upper end of
which the press cylinder is placed, at the same slope as the inclined plane,
and the ship is attached, by means of chains, to a crosshead fixed on the
plunger. Hydraulic power has also been used for launching ships, and the
launch of the Great Eastern is a memorable instance; for the great ship
stuck fast, and it was only by the application of an immense pressure,
exerted by hydraulic apparatus, that she could be induced to take to the
water. Water pressure is also applied to hoists for raising and lowering
heavy bodies, and in such cases the pressure which is obtained by simply
taking the water supply from an elevated source, or from the water-main
of a town, is sometimes made use of, instead of that obtained by a forcing
pump. The lift at the Albert Hall, South Kensington, by which persons
may pass to and from the gallery without making use of the stairs, is
worked by hydraulic pressure in the manner just mentioned. In such lifts
or hoists there is a vertical cylinder, in which works a leather-packed piston,
having a piston-rod passing upwards through a stuffing-box in the top of
the cylinder. The upper end of the piston-rod has a pulley of 30 in. or
36 in. diameter, attached to it, and round this pulley is passed a chain, one
end of which is fixed, and the other fastened to the movable cage or frame.
So that the cage moves with twice the speed of the piston, and the length
of the stroke of the latter is one-half of the range of the cage.
Sir William Armstrong has applied hydraulic power to cranes and other
machines in combination with chains and pulleys. His hydraulic crane
is represented by the diagram, Fig. 169, intended to show only the general
disposition of the principal parts of this machine, which is so admirably
arranged that one man can raise, lower, or swing round the heaviest load
with a readiness and apparent ease marvellous to behold. Here it is
proper to mention once for all, that the pressure for the hydraulic machines
is obtained not only by natural heads of water, or by forcing-pumps worked
by hand, but very frequently by forcing-pumps worked by steam power. It
is usual to have a set of three pumps with their plungers connected respectively
with three cranks on one shaft, making angles of 120° with each
334other. A special feature of Sir W. Armstrong’s hydraulic crane is the
arrangement by which the engines are made to be always storing up power
by forcing water into the vessel, a, called the “accumulator.” The accumulator—which
in the diagram is not shown in its true position—may be
placed in any convenient place near the crane, and consists of a large cast
iron cylinder, b, fitted with a plunger, c, moving water-tight through the neck
of the cylinder. To the head of the plunger is attached by iron cross-bars,
d d, a strong iron case filled with heavy materials, so as to load the plunger,
c, with a weight that will produce a pressure of about 600 lbs. upon each
square inch of the inner surface of the cylinder. The water is pumped into
the cylinder by the pumping engines through the pipe, f, and then the
piston rises, carrying with it the loaded case, guided by the timber framework,
g, until it reaches the top of its range, when it moves a lever that
cuts off the supply of steam from the pumping engine. When the crane is
working the water passes out of the cylinder, a, by the pipe, h, and exerts
its pressures on the plungers of the smaller cylinders; and the plunger of
the accumulator, in beginning its descent again, moves the lever in connection
with the throttle-valve of the engine, and thus again starts the
pumps, which therefore at once begin to supply more water to the accumulator.
The latter is, however, large enough to keep all the several
smaller cylinders of the machine at work even when they are all in operation
at once. Fig. 169 shows a sketch elevation and a ground plan of the
crane as constructed to carry loads of 1 ton, but the size of the cylinders
is somewhat exaggerated, and all details, such as pipes, guides, valves,
rods, &c., are omitted. The hydraulic apparatus is entirely below the
flooring—only the levers by which the valves are opened and closed appearing
above the surface. The crane-post, i, is made of wrought iron:
it is hollow and stationary; the jib, k, is connected with the ties, l, by side-pieces,
n, which are joined by a cross-piece at m, turning on a swivel and
bearing the pulley, u. The jib and the side-pieces are attached at o to a
piece turning round the crane-post, and provided with a friction roller, p,
which receives the thrust of the jib against the crane-post; the same piece
is carried below the flooring and is surrounded with a groove, which the
links of the chain, q, fit. This chain serves to swing the crane round, and
for this purpose the hydraulic cylinders, r, r´, come into operation. The
plungers of these have each a pulley, over which passes the chain q, having
its ends fastened to the cylinders, so that when, by the pressure of the
water, one plunger is forced out, the other is pushed in, and the chain
passing round the groove at s swings the jib round. The cylinders are
supplied with water by pipes—omitted in the sketch, as are also those by
which the water leaves the cylinders. These pipes are connected with
valves—also omitted on account of the scale of the diagram being too
small to show their details—so that the movement of a lever, t, in one or
the other direction at the same time connects one cylinder with the supply
and the other with the exit-pipe. When the crane is swinging round, the
sudden closing of the valves would produce an injurious shock, and to
prevent this relief-valves are provided on both the supply and exit-pipes
communicating with each cylinder. When, therefore, the valves are closed,
the impetus of the jib and its load acting on the chain, and through that
on the plungers, continues to move the latter, the motion is permitted to
take place by the relief-valves opening, and allowing water to enter or leave
the cylinders against the pressure of the water. There is also a self-acting
arrangement by which, when these plungers have moved to the extent of
335their range in either direction, the valves are closed. The chain of the
crane rests on guide pulleys, and passing over the pulley u, goes down the
centre of the crane-post to the pulley v, and thence passes backwards and
forwards over a series of three pulleys at w and two at x, and is fastened
at its end to the cylinder, y. As there are thus six lines of chain, when the
plunger of the lifting cylinder comes 1 ft. out, 6 ft. of chain pass over the
guide pulley, u. The plunger, when near the end of its stroke in either
direction, is made to move a bar—not shown—which closes the valve.
When the crane is loaded, the load is lowered by simply opening the
exhaust-valve, when the lift-plunger will be forced back into its cylinder
by the pull on the chain. But as the chain may require to be lowered
when there is no load upon it, although a bob is provided at z to draw the
336chain down, it would be disadvantageous to increase
the weight of this to the extent required
for forcing back the lifting plunger. A return
cylinder is therefore made use of, the plunger
of which has but a small diameter, and is connected
with the head of the lift-plunger, so that
it forces the latter back when the lift-cylinder
is put in communication with the exhaust-pipe.
The water is admitted to the lifting cylinder
from the accumulator by a valve worked by a
lever, which, when moved the other way, closes
the communication and opens the exhaust-pipe,
and then the pressure in the return cylinder,
which is constant, drives in the plunger of the
lifting cylinder. The principle of the accumulator
may plainly be used with great advantage
even when manual labour is employed, for a less
number of men will be required for working the
pumps to produce the effect than if their efforts
had to be applied to the machine only at the
time it is in actual operation, for in the intervals
they would, in the last case, be standing idle.
Apparatus on the same plan has been used with
advantage for opening and shutting dock gates,
moving swing bridges, turn-tables, and for other
purposes where a considerable power has to be
occasionally applied.
Fig. 169.—Sir W. Armstrong’s Hydraulic Crane.
Fig. 170.—Raising Tubes of the Britannia Bridge.
Fig. 171.—Press for Raising the Tubes.
Fig. 172.—Head of Link-Bars.
A famous example of the application of hydraulic
power was the raising of the great tubes
of the Britannia Bridge. As already stated, the
tubes were built on the shore, and were floated
to the towers. This was done by introducing beneath
the tubes a number of pontoons, provided
with valves in the bottom, so as to admit the
water to regulate the height of the tube according
to the tide. The great tubes were so skilfully
guided into their position that they appeared to
spectators to be handled with as much ease as
small boats. The mode in which they were raised
by the hydraulic presses wall be understood from
Fig. 170, where A is one of the presses and C the
tube, supported by the chains, B. The tubes were
suspended in this manner at each end, and as the
great tubes weighed 1,800 tons, each press had,
therefore, to lift half this weight, or 900 tons.
The ram or plunger of the pump was 1 ft. 8 in.
in diameter, and the cylinder in which it worked
was 11 in. thick. Two steam engines, each 40
horse-power, were used to force the water into
the cylinders. These cylinders were themselves
remarkable castings, for each contained no less
than 22 tons of iron. Notwithstanding the great
thickness of the metal, an unfortunate accident
337occurred while the plungers were making their fourth ascent, for the bottom
of one of the cylinders gave way—a piece of iron weighing nearly a ton and
a half having been forced out, which, after killing a man who was ascending
a rope ladder to the press, fell on the top of the tube 80 ft. below, and
made in it a deep indentation. The accident occasioned a considerable
delay in the progress of the work, for a new cylinder had to be cast and
fitted. Such an accident would assuredly have caused the destruction of
the tube itself but for the foresight and prudence of the engineer in placing
beneath the ends of the vast tube as it ascended slabs of wood 1 in. thick,
so that it was impossible for the tube to fall more than 1 in. It must be
stated that as the tube was lifted each step, the masonry was built up from
below, and then as the next lift proceeded inch by inch, a slab of wood was
placed under the ends. Although by the giving way of the cylinder of the
hydraulic press the end of the tube fell through no greater space than 1 in.,
the momentum was such that beams calculated to bear enormous weights
were broken. At the time of the accident the pressure in the cylinder did
not exceed that which it was calculated to bear or that which is frequently
applied in hydraulic presses for other purposes. Some scientific observers
attributed the failure of the cylinder to the oscillating of the tube. It had
338been found when the similar tubes of the bridge over the Conway were
being raised, that when the engines at each end made their strokes simultaneously,
a dangerous undulation was set up in the tube, and it was therefore
necessary to cause the strokes of the engines to take place alternately.
The chains by which the tubes were suspended were made of flat bars 7 in.
wide and about 1 in. thick, being rolled in one piece, with expanded portions
about the “eye,” through which the connecting-bolts pass. The links of
the chain consisted of nine and eight of these bars alternately—the bars of
the eight-fold links being made a little thicker than those of the nine-fold,
so as to have the same aggregate strength. The mode in which the
hydraulic presses were made to raise the tubes is very clearly described by
Sir William Fairbairn in his interesting work on the Conway and Britannia
Bridges, and his account of the mode of raising the tubes is here given
in his own words, but with letters referring to Fig. 171:
“Another great difficulty was to be overcome, and it was one which presented
itself to my mind with great force, viz., in what manner the enormous
weight of the tube was to be kept suspended when lifted to the height
of 6 ft., the proposed travel of the pump, whilst the ram was lowered and
again attached for the purpose of making another lift. Much time was
occupied in scheming means for accomplishing this object, and after examining
several projects, more or less satisfactory, it at last occurred to me
that, by a particular formation of the links (of the chain by which the
tubes were to be suspended) we might make the chains themselves support
the tube. I proposed that the lower part of the top of each link, immediately
below the eye, should be formed with square shoulders cut at right
angles to the body of the link (Fig. 172). When the several links forming
the chain E were put together, these shoulders formed a bearing surface, or
“hold,” for the crosshead B attached to the top of the ram A of the hydraulic
pump. But the upper part of this crosshead, C C, was movable, or formed of
clips, which fitted the shoulders of the chain, and were worked by means
of right- and left-handed screws, and could be made either to clip the chain
immediately under the shoulders when the ram of the pump was down and
a lift about to be made, or be withdrawn at pleasure. Attached to the large
girders F were a corresponding set of clips, D D, which were so placed and adjusted
as to height that when the ram of the pump was at the top there was
distance between the two sets of clips equal to twice the length of the travel
of the pump, or the length of the two sets of the links of the chain. To
339render the action of the apparatus more clear, suppose the tube resting on
the shelf of masonry in the position that it was left in after the operation
of floating was completed, and the chains attached, and everything ready
for the first lift, the ram of the pump being necessarily down. The upper
set of clips attached to the crosshead are forced under the shoulders of the
links, and the lower set of clips attached to the frames resting upon the
girders are drawn back, so as to be quite clear of the chain; the pumps are
put into action simultaneously at both ends of the tube, and the whole
mass is slowly raised until it has reached a height of 6 ft. from its original
resting-place. The clips attached to the crosshead, B, have so far been
sustaining the weight, but it will be observed that by the time the pump has
ascended to its full travel, the square shoulders of another set of links have
come opposite to the lower clips on the girders, D, and these clips are
advanced under the shoulders of the links, and the rams being allowed to
descend a little, they in their turn sustain the load and relieve the pumps.
The upper clips being withdrawn, the rams are allowed to descend, and
after another attachment, a further lift of 6 ft. is accomplished; and thus,
by a series of lifts, any height may be attained. The fitness of this apparatus
for its work was admirable, and the action of the presses was, as Mr.
Stephenson termed it, delightful.”
Fig. 173.—Apparatus to prove Transmission of Pressure in all directions.
340
Fig. 174.—Pneumatic Tubes and Carriages.
PNEUMATIC DISPATCH.
When the use of the electric telegraph became general, it was found
necessary to establish in all large towns branch stations, from which
messages were conveyed to the central station, or to which they were sent,
either by messengers who carried the written despatch, or by telegraphing
between the central and branch stations. The latter had the disadvantages
of rendering the original message liable to an additional chance of
incorrect transmission, and when an unusually great number of despatches
had to be sent to or from a particular branch station, there was necessarily
great delay in the forwarding of them. The plan of sending the written
messages between the central stations by bearers was unsatisfactory on
account of the time occupied. These inconveniences led to the invention
of a system for propelling, by the pressure of air, the papers upon which
the messages were written through tubes connecting the stations. This
was first carried into practice by the Electric and International Telegraph
Company, who, in this way, connected their central station in London with
their City branch stations. The apparatus was designed and erected by
Mr. L. Clark and Mr. Varley in 1854. The first tube laid down was from
Lothbury and the Stock Exchange—a distance of 220 yards. This tube
had an inside diameter of only 1½ in.; but a larger tube, having a diameter
of 2¼ in. was, some years afterwards, laid between Telegraph Street and
Mincing Lane—a distance of 1,340 yards—and was used successfully. In
341these tubes the carriers were pushed forward by the pressure of the atmosphere,
a vacuum having been produced in front by pumping out the air.
The plan of propelling the carrier by compressing the air behind it was
also tried with good results, and, in fact, with a gain of speed; for, while a
carrier occupied 60 or 70 seconds in passing from Telegraph Street to
Mincing Lane when drawn by a vacuum, it accomplished its journey in
50 or 55 seconds when it was shot forwards by compressed air, the difference
in pressure before and behind it being the same in each case. A
great deal of trouble was occasioned when the vacuum system was used,
by water being drawn in at the joints of the pipes. This water sometimes
accumulated to such a degree, especially after wet weather, that it completely
overcame the power of the vacuum to draw the air through it, by
lodging in the vertical portions of the tube, where they passed to the upper
floors of the central station. This was remedied by improving the construction
of the joints, and by arranging a syphon for drawing off any
water which might be present. The best construction of the carrier was
another matter which required some experience to discover. It was found
that gutta-percha, or papier maché covered with felt, was the most efficient
material. The tubes found by Mr. Varley to give the best results were
formed of lead covered externally with iron pipes. The joints were made
perfectly smooth in the inside by means of a heated steel mandrel, on which
they were formed, so that the tube was of one perfectly uniform bore
throughout. An ingenious arrangement was also adopted by which the air
itself was made to do the work of opening and closing the valves, and
even that of removing the carrier from the tube: when, by a telegraphic
bell, rung from the distant station, it was announced that a carrier was
dispatched, the attendant at the receiving station had only to touch for a
second a knob marked “receive,” which put the tube in communication
with the vacuum, in which condition it remained until the arrival of the
carrier, which, by striking against a pad of india-rubber, released the detent,
and thus cut off the vacuum. The carrier then fell out of the receiver
and dropped into a box placed to catch it. When a carrier was sent,
it was placed in the tube, and a button marked “send” was touched, by
which a communication was opened with a vessel of compressed air and the
end of the tube behind the carrier was immediately closed by a slide, the
movements being all performed by the air itself. On the arrival of the
carrier, the boy at the receiving station rang an electric bell to signal its
reception; and the sender then touched another knob marked “cut off,”
which caused the supply of compressed air to be cut off, and the slide to
be withdrawn from the end of the tube, which was then ready either to
receive or send carriers. By this arrangement there was no waste of power,
for the reservoirs of compressed air or of vacuum were only drawn upon
when the work was actually required to be done.
The tubes laid down by the Telegraph Company are still in active operation;
but at the new Central Telegraph Station the automatic valves of
Messrs. Clark and Varley appear to be dispensed with, and the attendants
perform the work of closing the tube, shutting off the compressed air, &c.,
by a few simple movements.
In December, 1869, Messrs. Siemens were commissioned by the Postmaster-General
to lay tubes on their system from the General Post Office
to the Central Telegraph Station; and the work having been accomplished
in February, 1870, and proving perfectly satisfactory after six weeks’ trial,
it was decided to connect in the same manner Fleet Street and the West
342Strand office at Charing Cross with the Central Station. The system
proposed by the Messrs. Siemens consisted in forming a circuit of tubes,
through which the carriers might be continually passing in one direction.
The diagram, Fig. 175, will give an idea of the manner in which it was
designed to arrange the tubes between the Central Telegraph Station and
Charing Cross. The arrows indicate the direction in which the air rushes
through the tubes; A is the piston in the cylinder, and valves are so
arranged as to pump air out of the chamber V, and compress it into the
chamber P. This plan has been departed from, so far as regards the
Charing Cross Station, for want of space there prevented the tube being
curved with a radius large enough to convey the carriers without their
being liable to stick, and consequently, these are not carried round in the
tube. The passage of carriers being stopped here, there are, in point of
fact, two tubes: an “up” tube and a “down” tube. But these are connected
by a sharp bend, so that though the tube is continuous as regards
the air current, it is interrupted as regards the circulation of the carriers.
The tubes are of iron, 3 in. internal diameter, made in lengths of about 19 ft.;
and for the turns and bends, pieces are curved with a radius of 12 ft. Both
lines are laid side by side in a trench at about a foot depth below the streets.
The ends of the adjacent lengths form butt joints, so that the internal surface
is interrupted as little as possible, and there is a double collar to fasten
the lengths together. Arrangements are also made for removing from the
inside of the tubes water or dirt, or matter which may in any manner have
got in.
Fig. 175.—Diagram of Tubes, &c.
Fig. 176.—Sending and Receiving Apparatus.—Transverse Section.
One special feature of Messrs. Siemens’ invention is the plan by which
the carriers are introduced into and removed from the tube at any required
station without the circulation of the air being interfered with. The simple
yet ingenious mechanism by which this is effected will be understood from
the sections shown in Figs. 176 and 177. The figures represent the position
of the apparatus when placed to receive a carrier; A´ is the receptacle
into which the carrier is shot by the air rushing from A towards A´´. This
receptacle is ᗜ-shaped, the curve of the Ⅾ corresponding with that of the
tube, and the upper flat part admitting of a piece of plate glass being inserted,
through which the attendant may perceive when a carrier arrives.
The progress of the carrier is arrested by a perforated plate, B, which
allows the air to pass. The ends of this receptacle are fixed in two parallel
plates, F F´, which also receive the ends of the plain cylinder, having precisely
the same diameter as the tube, A. These plates are connected also
343by cross-pieces, D E, the whole forming a sort of frame, which turns upon
E as a centre; and according as it is put in the position shown by the plain
line in Fig. 176, or in that indicated by the dotted lines, causes the receiving
tube or the hollow cylinder to form part of the main tube, the cross-piece,
D, serving as a handle for moving the apparatus. It should be remarked
that the plates are made to fit the space cut out of the main tube with great
nicety, otherwise much loss of power would result from leakage. When
the hollow cylinder is in a line with the main tube, it is plain that the
carrier will not be stopped, as the tube is then continuous and uninterrupted.
In this hollow cylinder also the carrier to be sent is deposited
after the rocking frame has been placed on it, Fig. 177; then, on drawing
the handle, the hollow cylinder is brought into the circuit, and the carrier
at once shoots off. To stop a carrier, the receiving-tube is put in by another
movement of the handle, and when the carrier arrives, it is removed by
bringing the open cylinder, or through tube, into the circuit, and thus
making the receiver ready for having the carrier pushed out of it by a rod
which is made to slide out by moving a handle. In order to avoid the
obstruction to the movement of the air which would be caused by the
carrier while in the receiving-tube, a pipe, G, is provided, through which
344the air chiefly passes when the perforations of the plate, B, are closed by
the presence of a carrier. In this pipe at H is a throttle-valve, which
is opened by tappets, K, on the rocking frames when the receiver is in
circuit, and again closed when the open tube is substituted. The current
thus suffers no interruption by the action of the apparatus.
The carriers are small cylinders of gutta-percha, or papier maché, closed
at one end, and provided with a lid at the other. They are covered with
felt or leather, and at the front they are furnished with a thick disc of
drugget or leather, like the leathers of a common water-pump, but fitting
quite loosely in the tube. Such a carrier, being placed in the tube at the
Central Station, Fig. 175, will be carried by the current in the direction of
the arrows to the Charing Cross Station, where its progress will be interrupted;
but according to the original plan it would continue its journey until
it again reached the Central Station, where it would be intercepted by the
diaphragm, Fig. 175. But the carrier is stopped, if at any station the receiving-tube
is placed in circuit, and this is done when an electric signal
indicates to the station that a carrier intended for it has been dispatched.
The tubes are worked on the “block system,” that is, each section is known
to be clear before a carrier is allowed to enter it, and a bell is provided,
which is struck by a little lever, moved by each carrier in its passage
through, so that the attendant at each station knows when a carrier has
shot along the “through tube” of the station. This mode of working the
tubes renders the liability to accidents much less, but their carrying power
might be increased by dispatching carriers at regular and very short intervals
of time, when the limit would be only in the ability of the attendants
to receive a carrier and open the circuit in sufficient time to allow the next
following one to proceed without stoppage. The length of the lines of tube
laid down on this system, with the times required for the carriers to traverse
them, are stated below, the pressure and the vacuum being respectively
equal to the absolute pressures of 22 lbs. and 5½ lbs. on each square inch
of the reservoirs during the experiments:
345
Yards.
M. S.
Telegraph Station to General Post Office
852
1 54
General Post Office to Temple Bar
1,206
2 28
Temple Bar to General Post Office
1,206
2 10
General Post Office to Telegraph Station
852
1 13
4,116
7 45
When the air was not compressed, but the vacuum only was used, the
air being allowed to enter the other end of the tube at the ordinary atmospheric
pressure, the time required for the carrier to traverse the circuit
was 10 minutes 23 seconds. In this case the vacuum was maintained, so
that the air was constantly in movement; but when the experiment was
tried by allowing the air in the tube to become stationary, placing a carrier
at one end, and then opening communication with the vacuum reservoir at
the other, the carrier required 13½ minutes to complete the journey. This
is explained by the fact of the greater part of the air having to be exhausted
from the tube before the carrier could be set in motion.
The utility and advantage of the pneumatic system is well seen when its
powers are compared with the wires. Thus, a single carrier, which may
contain, say, twenty-seven messages, can be sent every eight minutes; and
since not more than one message per minute could be transmitted by telegraph
wire, even by the smartest clerks, the real average being about two
minutes for each message, it follows that only four messages could be sent
in the time required for a single carrier to traverse the up tube, and to do
the work which could be done by the tube seven wires and fourteen clerks
would be required.
Mr. R. S. Culley, the official telegraph engineer, states as his experience
of the relative wear and tear of the carriers in these iron tubes and in
the smooth lead tubes, that it had been found necessary to renew the felt
covering of eighty-two dozen of the carriers used for three months in the
iron tubes, while in the same period only thirty-eight dozen of those used
in the lead tubes required to be recovered. The numbers of carriers
sent and received by the pneumatic tubes on the 21st of November, 1871,
between 11 a.m. and 4 p.m., were:
Iron tubes
135
2¼ in. lead tubes
1,170
1,697
1½ in. lead tubes
527
The mileage of the carriers sent was much greater in the lead than in
the iron pipes, although the total lengths of each kind were respectively
5,974 yards and 6,826 yards. The result is remarkable, as showing the
effect of apparently slight differences when their operation is summed up
by numerous repetitions.
The circuit at Charing Cross having been divided on account of the
difficulty mentioned above, the tubes act as separate pipes—one for “up”
traffic (i.e., to Central Telegraph Station), the other for “down” (i.e., from
the Central Station). The air, however, still accomplishes a circuit, being
exhausted at one end and compressed at the other. A very noticeable and
curious difference is found between the times required by the carriers to
perform the “up” and the “down” journeys:
346
An “up” carrier requires
6·5 minutes
A “down” carrier requires
12·5 minutes
Together
19·0 minutes
When two pipes were separated at Charing Cross so that the air no
longer circulated from one to the other, but both were left open to the
atmosphere, while the “up” pipe was worked by a vacuum only and the
“down” pipe by pressure only, the times were for
An “up” carrier
8·5 minutes
A “down” carrier
11·3 minutes
Together
19·8 minutes
The time, therefore, for the whole circuit was practically the same—whether
the tubes were worked by a continuous current of air or separated,
and one worked by the vacuum and the other by pressure. It was also
seen that when the tubes were connected so that the air current was continuous,
and the pump producing a vacuum at one end and a compression
at the other, the neutral point where the pressure was equal to that of the
atmosphere was not found midway between the two extremities—that is,
at Charing Cross Station—but much nearer the vacuum end. When the
tubes were disconnected, it appeared, as already shown by the figures given
above, that there was a gain of speed on the down journey, and a loss of
speed on the up journey; and as the requirements of the traffic happened
to require greater dispatch for the down journeys, the tubes have been
worked in this manner.
It has been proposed to convey letters by pneumatic dispatch between
the General and Suburban Post Offices, and the Post Office authorities
have even consulted engineers on the practicability of sending the Irish
mails from London to Holyhead by this system. It was calculated,
however, that although the scheme could be carried out, the proportion
of expense for great speeds and long distances would be enormously
increased. A speed of 130 miles per hour was considered attainable, but
the wear and tear of the carriers would be extremely great at this high
velocity, and it was considered doubtful whether this circumstance might
not operate seriously against the practical carrying out of the plan. The
prime cost would be very great, for the steam power alone which would be
requisite would amount to 390 horse-power for every four miles. We thus
see that very high velocities would introduce a new order of difficulties in
the practical working. The case as regards the velocity with which electric
signals can be sent round the world is very different.
An amusing hoax appears to have been perpetrated by some waggish
telegraph clerk on an American gentleman at Glasgow, with regard to the
pneumatic system of sending messages; for the gentleman sent to the
“Boston Transcript” a letter, in which he relates that having sent a telegraphic
message from Glasgow to London, he received in a few minutes a
reply which indicated a mistake somewhere, and then he went to the
Glasgow telegraph office, and asked to see his message.
“The clerk said, ‘We can’t show it to you, as we have sent it to London.’
‘But,’ I replied, ‘you must have my original paper here. I wish to see that.’
He again said, ‘No, we have not got it: it is in the post office at London.’
‘What do you mean?’ I asked. ‘Pray, let me see the paper I left here half
347an hour ago.’ ‘Well,’ said he, ‘if you must see it, we will get it back in a
few minutes, but it is now in London.’ He rang a bell, and in five minutes
or so produced my message, rolled up in pasteboard.... I inquired
if I might see a message sent. ‘Oh, yes; come round here.’ He slipped
a number of messages into the pasteboard scroll, popped it into the tube,
and made a signal. I put my ear to the tube and heard a slight rumbling
noise for seventeen seconds, when a bell rang beside me, indicating that
the scroll had arrived at the General Post Office, 400 miles off. It almost
took my breath away to think of it.”
In the journal called “Engineering,” into which this curious letter was
copied, it is pointed out that to travel from London to Glasgow, a distance
of 405 miles, in seventeen seconds, the carrier must have moved at the rate
of 24 miles per second, or 5 miles a second faster than the earth moves in
its orbit, and the carrier would have in such a case become red hot by its
friction against the tube before it had travelled a single second.
A plan of conveying, not telegraph messages, but parcels, was proposed
and carried into effect some time ago, and more recently has been applied to
lines of tubes in connection with the General Post Office. These tubes pass
from Euston Station down Drummond Street, Hampstead Road, Tottenham
Court Road, to Broad Street, St. Giles’s, whence, with a sharp bend,
they proceed to the Engine Station at Holborn, and then to the Post Office.
The tube is formed chiefly of cast iron pipes of a ⌓-shaped section, 4 ft. 6 in.
wide and 4 ft. high, in 9 ft. lengths. There are curves with radii of 70 ft.
and upwards, and at these parts the tube is made of brickwork and not of
iron. The carriages run on four wheels, and are so constructed that the
ends fit the tubes nearly, and the interval left is partly closed by a projecting
sheet of india-rubber all round. The carriages are usually sent through
the tube in trains of two or three, and the trains are drawn forward by an
exhausting apparatus formed by a fan, 22 ft. in diameter, worked by two
horizontal steam engines having cylinders 24 in. in diameter and a stroke
of 20 in. The air rushes by centrifugal force from the circumference of
the fan, and is drawn in at the centre, where the exhaust effect is produced.
The tubes which convey the air from the main tube open into the latter
at some distance from its extremities, which are closed by doors, so that
after the carriage passes the entrance of the suction tube, its momentum is
checked by the air included between it and the doors, which air is, of
course, compressed by the forward movement of the carriage. At the
proper moment the doors are opened by a self-acting arrangement, and the
carriage emerges from the tube. There are two lines of tube—an “up”
and a “down” line—and means are provided for rapidly transferring the
carriages from one to the other at the termini. The time occupied in the
transit is about 12 minutes. Some of the inclines have as much slope as
1 in 14, yet loads of 10 or 12 tons weight are drawn up these gradients without
difficulty. The mails are sent between Euston Station and the Post
Office by means of these tubes. Passengers have also made the journey as
an experiment by lying down in the carriages. Fig. 174 shows one of the
carriages and the entrance to the tubes.
Great expectations have been formed by some persons of the applications
of pneumatic force. Some have suggested its use for moving the
trains in the proposed tunnel between England and France. But calculations
show that for long distances and large areas such modes of imparting
motion are enormously wasteful of power. Thus, in the tunnel alluded
to it must be remembered that not only the train, but the whole mass of
348air in the tunnel would have to be drawn or pushed forward. The
drawing of a train through by exhausting the air would be very similar to
drawing it through by a rope; in fact, the mass of air may be regarded as
a very elastic rope, but by no means a very light one, or one that could be
drawn through without some opposing force which has a certain resemblance
to friction coming into operation. Indeed, it has been calculated
that in the case named, only five per cent. of the total power exerted by
the engines in exhausting the air could possibly produce a useful effect in
moving the train.
Air has also been made the medium for conveying intelligence in another
manner than by shooting written messages through tubes, for its property
of transmitting pressure has been applied to produce at a distance signals
like those made use of in the electric telegraph system. A few years ago,
an apparatus for this object was contrived by Signor Guattari, whose invention
is known as the “Guattari Atmospheric Telegraph.” In this there
is a vessel charged with compressed air by a compression-pump, and the
pressure is maintained by the same means, while the reservoir is being
drawn upon. A valve is so arranged that the manipulator can readily
admit the compressed air to a tube extending to the station where the
signals are received, at which the pressure is made to move a piston as
often as the sender opens the valve. This movement is made to convey
intelligence when a duly regulated succession of impulses is sent into the
tube—the receiving apparatus being arranged either to give visible or
audible signals, or to print them on slips of paper, according to any of the
methods in use with the electric telegraph. Certain advantages over the
electric system are claimed for this pneumatic telegraph—as, for example,
greater simplicity and less liability to derangement. The tubes, which are
merely leaden piping of small bore, are also exempt from the inconvenient
interruptions which electric communication sometimes suffers from electrical
disturbances in the atmosphere. The pneumatic system is easily
arranged, and from its great simplicity any person can in a few hours learn
to use the whole apparatus, while it is calculated that the expense of construction
and working would not be above half of that incurred for the
electric system. For telegraphs in houses, ships, warehouses, and short
lines, this invention will doubtless prove very serviceable; but for long
lines a much greater force of compression would be required, and the time
needed for the production of an impulse at the distant ends of the tubes
would be considerably increased. [1875].
349
Fig. 178.—The Sommeiller Boring Machines.
ROCK BORING. — THE MONT CENIS TUNNEL. — ROCK-DRILLING MACHINES. — THE CHANNEL TUNNEL. — THE ST. GOTHARD RAILWAY.
Allusion has already been made to one great characteristic of our
age, namely, the replacement, in every department of industry, of
manual labour by machines. A brief notice of even the main features of
the various contrivances which have been made to take the place of men’s
hands would more than occupy this volume. Accordingly, we must omit
all reference to many branches of manufacture, although the products may
be of very great utility, and the processes of very high interest; and in
taking one example here and another there, we must be guided mainly by
the extent and depth of the influence which the new invention appears
destined to exert. This consideration has, with scarcely an exception,
decided the selection of the topics already discussed, and it has also determined
the introduction of the present article, which relates to machines
of no less general importance than the rest, although at first sight it might
seem to enter upon the details of merely a special branch of industry. But
so general are the interests connected with the subject we are about to
lay before our readers, that we are not sure it would not have been more
logical to have placed the present article before all the rest. For whence
comes the iron of which our steam engines, tools, rails, ships, cannon,
bridges, and printing presses are made?—whence comes the fuel which
supplies force to the engines?—whence come, in fine, the substances
which form the matériel of every art? Plainly from the earth—the nurse
350and the mother of all, and in most cases from the bowels of the earth, for
her treasures are hidden far below the surface—the coal, and the ores of
iron and other metals, are not ready to our hand, exposed to the light of
day. The railways also, and the canals, can be made only on condition that
we cut roads through the solid rocks, and pierce with tunnels the towering
mountains. Hence the tools which enable us to penetrate into the substance
of the earth present the highest general interest from a practical
point of view, and this interest is enhanced by the knowledge of the structure
and past history of our planet acquired in such operations.
The operations by which solid rocks are penetrated in the sinking of
shafts for mines, or in the driving of tunnels, drifts, headings, galleries, or
cuttings for railways, mines, or other works, are easily understood. In the
first place a number of holes—perhaps 3 ft. or 4 ft. deep and 2 in. or 3 in. in
diameter—are formed in the rock. The holes are then charged with gunpowder
or other explosive materials, a slow-burning match is adjusted, the
miners retire to a safe distance, the explosion takes place—detaching,
shattering, and loosening masses of the rock more or less considerable; and
then gangs of workmen clear away the stones and débris which have been
detached by the explosion, and the same series of operations is renewed.
The holes for the blasting charges are formed by giving repeated blows
on the rock with a kind of chisel called a jumper—the end of which is
formed of very hard steel, so that the rock is in reality chipped away. The
débris resulting from this operation is cleared away from time to time by
a kind of auger or some similar contrivance. But for many purposes it is
necessary to drill holes in rocks to great depths, hundreds of feet perhaps,
as for example, in order to ascertain the nature of underlying strata, or to
verify the presence of coal or other minerals before the expense of sinking
a shaft is incurred. These bore-holes were commonly formed in exactly
the same manner as the blast-holes already mentioned, by repeated blows
of a chisel or jumper, which was attached to the end of a rod; and as the
hole deepened, additional lengths of rod were joined on, and the rods were
withdrawn from time to time to admit of the removal of the débris by
augers, or by cylinders having a valve at the bottom. The reciprocating
movement is given to the chisels and rods either by hand or by steam or
water power. When the length of the rods becomes considerable, of course
the difficulty of giving the requisite blows in rapid succession is greatly
increased, for the whole length of rods has to be lifted each time, and if
allowed to fall with too much violence, the breaking of the chisel or the
rods is the inevitable result. The time requisite for drawing out the rods,
removing the fragments chipped out, and again attaching the rods and
lowering, also increases very much as the bore gets deeper. Messrs.
Mather and Platt, the Manchester engineers, have, in order to obviate
these difficulties, constructed machines in which the chipping or cutting is
done by the fall of a tool suspended from a rope, the great advantage resulting
from the arrangement being the facility and rapidity with which
the tools used for the cutting and for the removal of the débris are lowered
to their work and drawn up. It is necessary in using the jumper, whether
in cutting blast-holes or bore-holes, to give the tool a slight turn after each
blow, in order that the rock may be chipped off all round, and the action of
the tool equalized. Many attempts have been made to drill rocks after the
fashion in which iron is drilled—that is, by drilling properly so called, in
which the tool has a rapid rotary motion. But even in comparatively soft
rock, it is found that no steel can sufficiently withstand the abrading action
351of the rock, for the tool becomes quickly worn, and makes extremely slow
progress. We shall have presently to return to the subject of bore-holes;
but now let us turn our attention to an example which will illustrate the
nature and advantages of the machinery which has in recent times been
applied to work the jumpers by which the holes for blasting are formed.
The successful construction, by the direction of Napoleon, of a broad and
easy highway from Switzerland into Italy, crossing the lofty Alps amid
the snows and glaciers of the Simplon, has justly been considered a feat of
skill redounding to the glory of its designers. But we have recently witnessed
a greater feat of engineering skill, for we have seen the Alps conquered
by the stupendous work known as the Mont Cenis Tunnel. This
tunnel is 7½ English miles in length; but it is not the mere length which
has made the undertaking remarkable. The mountain which is pierced by
the tunnel is formed entirely of hard rock, and what added still more to
the apparently impracticable character of the proposal when first announced
was the circumstance that it was quite impossible to sink vertical shafts, so
that the work could not, as in the usual process, be carried on at several
points simultaneously, but must necessarily be continued from the two
extremities only, a restriction which would occasion a vast loss of time and
much expense, to say nothing of the difficulties of ventilating galleries of
more than three miles in length. The reader must bear in mind that the
importance of this question of ventilation depends not simply on the renewing
of the air contaminated by the respiration of the workmen, but on
the quick removal of the noxious gases produced in the explosions of the
blasting charges. A work surrounded by such difficulties would probably
have never been attempted had not Messrs. Sommeiller and Co. invited
the attention of engineers to an engine of their invention, worked by compressed
air, and capable of automatically working “jumpers” which could
penetrate the hardest rock. These rock-boring machines, having been examined
by competent authorities in the year 1857, were pronounced so
efficient that the execution of the long-spoken-of Alpine tunnel was at once
resolved upon, and before the close of that year the work had actually been
commenced, after a skilful and accurate survey of the proposed locality
had been made, and the direction of the tunnel set out. The tunnel does
not pass through Mont Cenis, although the post road from St. Michel to
Susa passes over part of Mont Cenis, which gives its name to the pass.
The mountain really pierced by the tunnel is known as the Grand Vallon,
and the tunnel passes almost exactly below its summit, but at a depth the
perpendicular distance of which is as nearly as possible one mile. The
northern end of the tunnel is near a village named Fourneaux.
Pending the construction of the Sommeiller machines, and other machinery
which was to supply the motive force, the work of excavation was
commenced at both ends, in 1857, in the ordinary manner, that is, by hand
labour, and in 1858 surveys of the greatest possible accuracy were meanwhile
made, in order that the two tunnels might be directed so that they
would meet each other in the heart of the mountain. The reader will at
once perceive that the smallest error in fixing on the direction of the two
straight lines which ought to meet each other would entail very serious
352consequences. The difficulties of doing this may be conceived when we
remember that the stations were nearly 8 miles apart, separated by rugged
mountains, in a region of snows, mists, clouds, and winds, over which the
levels had to be taken, and a very precise triangulation effected. So successfully
were these difficulties overcome, and so accurately were the measurements
and calculations made, that the junction of the centre lines of
the completed tunnel failed by only a few inches, a length utterly insignificant
under the conditions.
The work was carried on by manual labour only, until the beginning
of 1861, for it was found, on practically testing the machinery, that many
important modifications had to be made before it could be successfully employed
in the great work for which it was designed. After the machinery
had been set to work, at the Bardonnêche end, breakages and imperfections
of various parts of the apparatus, or the contrivances for driving it,
caused delay and trouble, so that during the whole of 1861 the machines
were in actual operation for only 209 days, and the progress made averaged
only 18 in. per day, an advance much less than could have been effected
by manual labour. The engineers, not disheartened or deterred by these
difficulties and disappointments, encountered them by making improvement
after improvement in the machinery as experience accumulated, so
that a wonderful difference in the rate of progress showed itself in 1862,
when the working days numbered 325, and the average rate of advance
was three feet nine inches per day.
At the Fourneaux extremity more time was required for the preparation
of the air-compressing machinery, and the machines had been at work in
the other extremity, with more or less interruption, for nearly two years
before the preparations at Fourneaux were completed.
The illustration at the head of this article, Fig. 178, represents the Sommeiller
machines at work, the motive power being compressed air, conveyed
by tubes from receivers, into which it is forced until the pressure becomes
equal to that of six atmospheres, or 90 lbs. per square inch. The compression
was effected by taking advantage of the natural heads of water,
which were made to act directly in compressing the air; the pressure due
to a column of water 160 ft. high being made to act upwards, to compress
air, and force it through valves into the receivers; then the supply of water
was cut off, and that which had risen up into the vessel previously containing
air was allowed to flow out, drawing in after it through another
valve a fresh supply of air; and then the operations were repeated by the
water being again permitted to compress the air, and so on, the whole of
the movements being performed by the machinery itself. The compressed
air, after doing its work in the cylinders of the boring tools, escaped into
the atmosphere, and in its outrush became greatly cooled, a circumstance
of the greatest possible advantage to the workmen, for otherwise, from the
internal warmth of the earth, and that produced by the burning of lights,
explosions of gunpowder, and respiration, the heat would have been intolerable.
At the same time, the escaping air afforded a perfect ventilation
of the workings while the machines were in action. At other times, as after
the explosion of the charges, it was found desirable to allow a jet of air to
stream out, in order that the smoke and carbonic acid gas should be quickly
cleared away. Even had the work been done by manual labour alone, a
plentiful supply of compressed air would have been required merely for
ventilation, so that there was manifest advantage in utilizing it as the
motive power of the machines.
353
Fig. 179.—Transit by Diligence over Mont Cenis.
The experience gained in the progress of the work suggested from time
to time many improvements in the machinery and appliances, which finally
proved so effectual that the progress was accelerated beyond expectation.
At the end of 1864, when the machines had been in work about four years,
it was calculated that the opening of the tunnel might be looked for in the
course of the year 1875. But in point of fact it happened that on the 25th
December, 1870, perforator No. 45 bored a hole from Italy into France, by
piercing the wall of rock, about 4 yards thick, which then separated the
workings from each other. The centre lines of the two workings, as set
out from the different sides of the mountain, failed to coincide by only a
foot, that set out on the Fourneaux side being this much higher than the
other, but their horizontal directions exactly agreeing. The actual length
of the tunnel was found to be some 15 yards longer than the calculated
length, the calculation having given 7·5932 miles for the length, whereas by
actual measurement it was found to be 7·6017 miles. The heights above
the sea-level of the principal points are these:
Feet.
Fourneaux, or northern entrance
3,801
Bardonnêche, or southern entrance
4,236
Summit of tunnel
4,246
Highest point of mountain vertically over the tunnel
9,527
354The tunnel is lined with excellent brick and stone arching, and it is connected
with the railways on either side by inclined lines, which are in part
tunnelled out of the mountain, so that the extremities of the tunnel referred
to above are not really entered by the trains at all; but these lateral tunnels
join the other and increase the total distance traversed underground to
very nearly 8 miles, or more accurately, 7·9806 miles. The time required
by a train to pass from one side to the other is about 25 minutes. What a
contrast is this to the old transit over the Mont Cenis pass by “diligence”!
We have the scene depicted in Fig. 179, where we perceive, sliding down
or toiling up the steep zigzag ascents, a series of curious vehicles drawn by
horses with perpetually jingling bells.
The cost of the Mont Cenis Tunnel was about £3,000,000 sterling, or
upwards of £200 per yard; but as a result of the experience gained in this
gigantic work, engineers consider that a similar undertaking could now be
carried out for half this cost. It is supposed that the profit to the contractors
for the Mont Cenis Tunnel was not much less than £100 per yard.
The greatest number of men directly employed on the tunnel at one time
was 4,000, and the total horse-power of the machinery amounted to 860.
From 1857 to 1860, by hand labour alone, 1,646 metres were excavated;
from 1861 to 1870 the remaining 10,587 metres were completed by the
machines. The most rapid progress made was in May, 1865, in which
month the tunnel was driven forward at one end the length of 400 feet.
When the workings were being carried through quartz, a very hard rock,
the speed was greatly reduced—as, for example, during the month of April,
1866, when the machines could not accomplish more than 35 ft.
The perforators used in the Mont Cenis Tunnel were worked by compressed
air, conveyed to a small cylinder, in which it works a piston, to the
rod of which the jumper is directly attached. The air, being admitted behind
the piston, impels the jumper against the rock, and the tool is then
immediately brought back by the opening of a valve, which admits compressed
air in front of the piston, at the same time that the air which has
driven it forward is allowed to escape, communication with the reservoir
of compressed air having previously been closed behind it. The whole
of these movements are automatic, and they are effected in the most
rapid manner, four or five blows being struck in every second, or between
two and three hundred in one minute. Water was constantly forced into
the holes, so as to remove the débris as quickly as it was formed. A number
of these machines were mounted on one frame, supported on wheels, running
on the tramway which was laid along the gallery. The perforators had
no connection with each other, for each one had its own tube for the conveyance
of compressed air, and its own tube to carry the water used for
clearing out the hole, and the cylinders were so fixed on the frames that
the jumpers could be directed in any desired manner against any selected
portion of the rock. They were driven to an average depth of about 2½ ft.,
and the process occupied from forty to fifty minutes. When a set of holes
had thus been formed, the cylinders were shifted and another series commenced,
until about eighty holes had been bored, the formation of the
whole number occupying about six or seven hours, and the holes being so
arranged that the next operation would detach the rock to the required
extent. The flexible tubes, which conveyed the air and water to the machines
from the entrances, were then removed from the machines and
stowed away, the frame bearing the perforators was drawn back along the
tramway, workmen advanced whose duty it was to wipe out the holes,
355charge them with powder, and fix the fuses ready for the explosion. When
the slow-burning match was ignited, all retired behind strong wooden barricades,
at a safe distance, until the explosion had taken place; and after
the compressed air had been allowed to stream into the working, so as to
clear away all the smoke and gas generated by the explosion, the workmen
ran up on a special tramway the waggons which were to carry away all
the detached stones; and when this had been done, the floor was levelled,
the tramways were lengthened, and the frame bearing the drilling machines
was brought up to begin a fresh series of operations, which were usually
repeated about twice in the course of every twenty-four hours. A great part
of the rock consists of very hard calcareous schist, interspersed with veins
of quartz, one of the hardest of all rocks, which severely tries the temper
of the steel tools, for a few blows on quartz will not unfrequently cause the
point of a jumper to snap off.
Several forms of rock-drills, or perforators, have been constructed on
the same principle as that used in the Mont Cenis Tunnel, and a description
of one of them will give a good notion of the general principle of all.
We select a form devised by Mr. C. Burleigh, and much used in America,
where it has been very successfully employed in driving the Hoosac Tunnel,
effecting a saving in the cost of the drilling amounting to one-third of the
expense of that operation, and effecting also a still greater saving of time,
for the tunnel, which is 5 miles in length, is to be completed in four years,
instead of twelve, as the machines make an advance of 150 ft. per month,
whereas the rate by hand labour was only 49 ft. per month. These machines
are known as the “Burleigh Rock Drills,” and have been patented
in England for certain improvements by Mr. T. Brown, who has kindly
supplied us with the following particulars:
Fig. 180.—Burleigh Rock Drill on Tripod.
The Burleigh perforator acts by repeated blows, like Bartlett and Sommeiller’s,
but its construction is more simple, and the machine is lighter
and not half the size, while its action is even superior in rapidity and force.
The Burleigh machines are composed of a single cylinder, the compressed
air or steam acting directly on the piston, without the necessity of flywheel,
gearing, or shafting. The regular rotation of the drills is obtained
by means of a remarkably simple mechanical contrivance. This consists
of two grooves, one rectilinear, the other in the form of a spiral cut into the
piston-rod. In each of these channels, or grooves, is a pin, which works
freely in their interior: these pins are respectively fixed to a concentric
ring on the piston-rod. A ratchet wheel holds the ring, and the pin slides
into the curve, causing it to turn always in the same direction, without
being able to go back. By this eminently simple piece of mechanism, the
regular rotation of the drill-holder is secured. The slide-valve is put into
motion by the action of a projection, or ball-headed piston-rod, on a double
curved momentum-piece, or trigger, which is attached to the slide-rod or
spindle by a fork, thus opening and shutting the valve in the ascent and
descent of the piston. Fig. 180 represents one of the machines attached
in this instance by a clamp to the frame of a tripod. The principal parts
356of the machine are the cylinder, with its piston, and the cradle with guide-ways,
in which the cylinder travels. The action of the piston is similar to
that of the ordinary steam hammer, with this difference, that, in addition
to the reciprocating, it has also a rotary, motion. The drill-point is held in
a slip-socket, or clamp, at the end of the piston-rod, by means of bolts and
nuts. The drill-point rotates regularly at each stroke of the piston, making
a complete revolution in every eighteen strokes. For hard rocks it is generally
made with four cutting edges, in the form of a St. Andrew’s cross,
357thus striking the rock in seventy-two places in one revolution, each cutting
edge chipping off a little of the stone at each stroke in advance of the
one preceding. The jumper makes, on an average, 300 blows per minute,
and such is the construction of the machine, that the blows are of an
elastic, and not of a rigid, nature, thus preventing the drill-point from being
soon blunted. It has been found in practice, that a drill-point used in the
Burleigh machine can bore on an average 20 ft. of Aberdeen granite without
re-sharpening. As the drill pierces the rock, the machine is fed down
the guide-ways of the cradle by means of the feed-screw (see Fig. 180),
according to the nature of the rock and the progress made. When the
cylinder has been fed down the entire length of the feed-screw, and if
a greater depth of hole is required, the cylinder is run back, and a longer
drill is inserted in the socket at the end of the piston-rod. The universal
clamp may be attached to any form of tripod, carriage, or frame, according
to the requirements of the work to be done; it enables the machines to
work vertically, horizontally, or at any angle.
The following advantages are claimed for this machine: Any labourer
can work it; it combines strength, lightness, and compactness in a remarkable
degree, is easily handled, and is not liable to get out of order. No
part of the mechanism is exposed; it is all enclosed within the cylinder, so
there is no risk of its being broken. It is applicable to every form of rockwork,
such as tunnelling, mining, quarrying, open cutting, shaft-sinking, or
submarine drilling; and in hard rock, like granite, gneiss, ironstone, or
quartz, the machine will, according to size, progress at the incredible rate
of four inches to twelve inches per minute, and bore holes from ¾ in. up to
5 in. diameter. It will, on an average, go through 120 ft. of rock per day,
making forty holes, each from 2 ft. to 3 ft. deep, and it can be used at any
angle and in any direction, and will drill and clear itself to any depth up
to 20 ft.
The following extract from the “Times,” September 24th, 1873, gives an
account of some experiments with the machine, made at the meeting of
the British Association in that year, before the members of the Section
of Mechanical Science:
“Yesterday, considerable interest was taken in this section, as it had
been announced that a ‘Burleigh Rock Drilling Machine’ would be working
during the reading of a paper by Mr. John Plant. The machine was
not, however, in the room, but was placed in the grounds outside, where it
was closely examined by the members after the adjournment, and seen in
full operation, boring into an enormous block of granite. The aspect of the
machine cannot be called formidable in any respect, for it looks like a big
garden syringe, supported upon a splendid tripod; but when at work, under
about 80 lbs. pressure of compressed air, it would be deemed a very revolutionary
agent indeed, against whose future power the advocates for manual
labour in the open quarry, the tunnel, and even the deep mine, may well
look aghast. Placed upon a block of granite a yard deep, the machine was
handled and its parts moved by the fair hands of many of the lady associates
of scientific proclivities; but once the source of power was turned on,
the drill began its poundings, eating holes 2 in. in diameter in the block
of granite, and making a honeycomb of it as easily as a schoolboy would
demolish a sponge cake. It pounds away at the rate of 300 strokes, and
progresses forward about 12 in., in the minute, making a complete revolution
of the drill in eighteen strokes, and keeping the hole free of the
pounded rock. The machine was fixed to work at any angle, almost as
358readily as a fireman can work his hose; and its adaptation to a wide range
of stone-getting, by drilling for blasting, and cutting large blocks for building
and engineering, with a saving of capital and labour, was admitted by
many members of the section. The tool is called the ‘Burleigh Rock
Drill,’ invented by Mr. Charles Burleigh, a gentleman hailing from Massachusetts,
United States. The patent is the property of Messrs. T. Brown
and Co., of London. The principal feature of this new machine is, that it
imitates in every way the action of the quarryman in boring a hole in the
rock.”
Fig. 181.—Burleigh Rock Drill on Movable Column.
Many forms of carriages and supports have, from time to time, been
made to suit the work for which the ‘Burleigh’ machines have been
required. The machine is attached to these carriages, or supports, by
means of the universal clamp, by which it can be worked in any direction
and at any angle. Of these carriages we select for notice only two forms,
one of which is shown in Fig. 181. This carriage can be used to great
359advantage in adits and drifts. It consists of an upright column, with a
screw clamp-nut for holding and raising or lowering the machine, the
whole being mounted on a platform which can slide right across the
carriage, and thus the machine can be brought to work on any point of a
heading. It is secured in position by means of a jack-screw in the top of
the column; and as the carriage is mounted on wheels, it is easily moved
to permit of blasting. Fig. 182 represents a carriage which is the result of
many years’ experience with mining machinery, and it is considered a very
perfect appliance. It is constructed of wood and iron, and it runs on wheels.
The supports for the machines, four of which may be mounted at once, are
two horizontal bars, the lower of which can be raised or lowered, as may
be necessary. The two parallel sides of the carriage are joined only at the
upper side, and there is nothing to prevent it from being run into the heading,
though the way between the rails may be heaped up with broken rock,
if only the rails are clear. Drilling, and the removal of the broken rock,
may then proceed simultaneously; for, by means of a narrow gauge inside
the carriage rails, small cars may be taken right up to the débris. It is
made in different sizes, to suit the dimensions of the tunnel required. To
give the carriage steadiness in working, it is raised from the wheels by
jack-screws, and held in position by screws in a similar manner to the carriage
represented in Fig. 181.
Fig. 182.—Burleigh Rock Drills mounted on a Carriage.
Fig. 183.
An extremely interesting system of drilling rocks—totally different from
that on which the machines we have just described are constructed—has,
within the last few years, been introduced by Messrs. Beaumont and
Appleby. What does the reader think of boring holes in rocks with diamonds?
It has long been a matter of common knowledge that the diamond
360is the hardest of all substances, and that it will scratch and wear
down any other substances, while it cannot itself be scratched or worn by
anything but diamond. In respect to wearing down or abrading hard stones,
the diamond, according to experiments recently made by Major Beaumont,
occupies a position over all other gems and minerals to a degree far beyond
that which has been generally attributed to it; for in these experiments it
was found that on applying a diamond, or rather a piece of the “carbonate”
about to be described, fixed in a suitable holder, to a grindstone in rapid
rotation, the grindstone was quickly worn down; but on repeating a similar
experiment with sapphires and with corundum, it was these which were
worn down by the grindstone. Without, on the present occasion, entering
into the natural history of the diamond, we may say that there are, besides
the pure colourless transparent crystals so highly prized as gems, several
varieties of diamond, and that those which are tinged with pink, blue, or
yellow, are far from having the same value for the jeweller. Then there is
another impure variety called boort, which appears to be employed only to
furnish a powder by which the brilliants are ground and polished. In the
diamond gravels of Brazil, from which we derive our regular supply of these
gems, there was discovered in 1842 a curious variety of dark-coloured
diamond, in which the crystalline cleavage, or tendency to split in certain
directions (which belongs to the ordinary stones), appears to be almost
absent; and the substance might be regarded as a transition form between
the diamond and graphite but for its hardness. This substance was until
lately used for the same purposes as boort, which is a nearer relative of the
pure crystal, and like it, splits along certain planes. It received from the
miners the name of “carbonado,” and with regard to the application we are
considering, it has turned out to be a sort of Cinderella among diamonds;
for its unostentatious appearance is more than compensated for by its
surpassing all its more brilliant sisters in the useful property to which reference
has been made. This Brazilian term is doubtless the origin of
the English name by which the substance in question is known among
the English diamond merchants, who call it “carbonate”—an unfortunate
word, for it is used in chemistry with an entirely
different signification. “Carbonate” it is, however,
which supplies the requirements of the rock-drill,
and the selected stones are set in a crown,
or short tube, of steel, represented by c in Fig.
183. In this they are secured as follows: holes
are drilled in the rim of the tube, and each hole
is then cut so that a piece of the diamond exactly
fits it, and when this piece has been inserted, the
metal is drawn round by punches, so as almost
to cover the stone, leaving only a point projecting,
b b. The portions of the crown between the stones
are somewhat hollowed out, as at a, for a purpose
which will presently be mentioned. The crown
thus set with the boring gems is attached to the
end of a steel tube, by which it is made to rotate
with a speed of about 250 revolutions per minute while pressed against the
rock to be bored. Water is forced through the steel tube, and passing out
between the rock and the crown, especially under the hollows, c c, makes
its escape between the outside of the boring-tube and the rock, thus washing
away all the débris and keeping the drill cool. The pressure with
361which the crown is forced forward depends, of course, on the nature of the
rock to be cut, and varies from 400 lbs. to 800 lbs. In this way the hardest
rocks are quickly penetrated—sometimes, for example, at the rate of 4 in.
per minute, compact limestone at 3 in., emery at 2 in., and quartz at the rate
of 1 in. per minute. It is found that, even after boring through hundreds
of feet of such materials, the diamonds are not in the least worn, but as
fit for work as before: they are damaged only when by accident one of the
stones gets knocked out of its setting; and this machine surpasses all in the
rapidity with which it eats its way through the firmest rocks. This, it must
be observed, is the special privilege of the diamond drill—that, since the
begemmed steel crown and the boring-rods are alike tubular, the rock
is worn away in an annular space only, and a solid cylinder of stone is
detached from the mass, which cylinder passes up with the hollow rods,
where, by means of certain sliding wedges, it is held fast, and is drawn
away with the rods.
When the diamond drill is used merely for driving the holes for blasting,
this cylinder of rock is not an important matter; but there is an application
of the drill where this cylinder is of the greatest value, furnishing as it does
a perfect, complete, and easily preserved section of the whole series of
strata through which the drill may pass when a bore-hole is sunk in the
operation of searching for minerals (which is so significantly called in the
United States “prospecting,” a phrase which seems to be making its way
in England in mining connections); for the core is uniformly cylindrical,
the surface is quite smooth, and any fossils which may be present come up
uninjured, so far as they are contained in the solid core, and thus the strata
are readily recognized. Contrast this with the old method, where the bore-hole
in prospecting is made by the reciprocating action imparted to a steel
tool, and merely the pounded material is obtained, usually in very small
fragments, by augers or sludge-pumps: the fossils, which might afford the
most valuable indications, crushed and perhaps incapable of being recognized;
and instead of the beautifully definite and continuous cylinder, a
mere mass of débris is brought up. In the prospecting-bores the diameter
of the hole is from 2 in. to 7 in. The size adopted depends on the nature
of the strata to be penetrated, and on the depth to which it is proposed to
carry the boring. When the strata are soft, the operation is commenced
with a bore of 7 in., and when this has been carried to an expedient depth,
the danger of the sides of the hole falling in is avoided by putting down
tubes, and then the diamond drill, fixed to tubes of a somewhat smaller
diameter, will be again inserted, and the boring recommenced; or the hole
can be widened, so as to receive the lining-tubes. Of course, in boring
through hard rocks, such as compact limestones, sandstone, &c., no lining-tubes
are necessary.
In a very interesting paper, read before the members of the Midland
Institute of Mining Engineers, by Mr. J. K. Gulland, the engineer of the
Diamond Rock-Boring Company, who have the exclusive right of working
the patents for this remarkable invention, that gentleman concludes by
remarking that “the leading feature of the diamond drill is that it works
without percussion, thus enabling the holing of rocks to be effected by a far
simpler class of machinery than any which has to strike blows. Every
mechanical engineer knows, often enough to his cost, that he enters upon
a new class of difficulties when he has to recognize it as a normal state of
things with any machinery he is designing that portions of it are brought
violently to rest. These difficulties increase very much when the power, as
362in the case of deep bore-holes, has to be conveyed for a considerable distance.
Where steel is used a percussive action is necessitated, as, if a
scraping action is used, the drill wears quicker than the rock. The extraordinary
hardness of the diamond places a new tool in our hands, as its
hardness, compared with ordinary rock, say granite, is practically beyond
comparison. Putting breakages on one side, a piece of “carbonate” would
wear away thousands of times its own bulk of granite. Irrespective of the
private and commercial success which this invention has attained, it is a
boon to a country such as ours, where minerals constitute in a great measure
our national wealth and greatness.”
The advantages of the diamond drill may be illustrated by the case of
what is termed the Sub-Wealden Exploration. From certain geological
considerations, which need not be entered upon here, several eminent
British and continental geologists have arrived at the conclusion that it is
probable that coal underlies the Wealden strata of Kent and Sussex, and
that it may be perhaps met with at a workable depth. If such should really
prove to be the case, the industrial advantages to the south of England
would be very great, for the existence of coal so comparatively near to the
metropolis would prove not only highly lucrative to the owners of the coal,
but confer a direct benefit upon thousands by cheapening the cost of fuel.
A number of property owners and scientific men, having resolved that the
matter should be tested by a bore, raised funds for the purpose, and a 9 in.
bore had been carried down to a depth of 313 ft. in the ordinary manner,
when a contract was entered into with the Diamond Rock-Boring Company
for a 3 in. bore extracting a cylinder of rock 2 in. in diameter. The
company, as a precautionary measure, lined the old hole with a 5 in. steel
tube; and in spite of some delay caused by accidents, they increased the
depth of the hole to 1,000 ft. in the interval from 2nd February, 1874, to
18th June, 1874–-the progress of the work being regarded with the greatest
interest by the scientific world. Unfortunately, the further progress of the
work has been prevented by an untoward event, namely, the breaking of
the boring-rod, or rather tube; and, although the company is prepared
with suitable tackle for extracting the tubes in case of accidents of this
kind, and generally succeeds in lifting them by a taper tap, which, entering
the hollow of the tube, lays hold of it by a few turns—yet, in this instance,
where there have been special difficulties, the extraction of so great a
length of tubes is, as the reader may imagine, by no means an easy task.
Six attempts have been made to remove the boring-rods which have
dropped down; but so difficult has this operation proved, that, all these
efforts having failed, it has been decided to abandon the old work and
commence a new boring on an adjacent spot. A contract has been entered
into with the Diamond Boring Company, who have undertaken to complete
the first 1,000 ft. for £600, which is only £200 more than it would
have cost to completely line the old bore-holes with iron tubes—an operation
which was contemplated by the committee in charge of the exploration.
The terms agreed to by the company are very favourable to the promoters
of the Sub-Wealden Exploration, although the cost of the second 1,000 ft.
will be £3,000 more; and the committee are relying upon the public for
contributions to enable them to carry on their enterprise. It is most probable
that funds will be forthcoming, and should the boring result in the
finding of coal measures beneath the Wealden strata, all the nation will be
the richer and participate in the advantages resulting from an undertaking
carried on by private persons. Already a totally unexpected source of
363wealth has been met with by the old bore showing the existence of considerable
beds of gypsum in these strata, and the deposits of gypsum are
about to be worked. Whether coal be found or not found, there is no doubt
that a bore-hole going down 2,000 ft. will greatly increase our geological
knowledge, and may reveal facts of which we have at present no conception.
Fig. 184.—The Diamond Drill Machinery for deep Bores.
The boring-tubes, it maybe remarked, are made in 6 ft. lengths, and are
so contrived that the joints are nearly flush—that is, there is no projection
364at the junctions of the tubes. Fig. 184 is engraved from a photograph of
the machinery used for working the diamond drill when boring a hole for
“prospecting.” This looks at first sight a very complicated machine, but
in reality each part is quite simple in its action, and is easily understood
when its special purpose has been pointed out. We cannot, however, do
more than indicate briefly the general nature of the mechanism. The
reader will on reflection perceive that, although the idea of causing a rod
to rotate in a vertical hole may be simple, yet in practically carrying it out
a number of different movements and actions have to be provided for in
the machinery. The weight of the rods cannot be thrown on the cutters,
nor borne by the moving parts of the machine—hence the movable disc-shaped
weights attached to the chains are to balance the weight of the
boring-rods as the length of the latter is increased. There must also be a
certain amount of feed given to the cutters, regulated and adjusting itself
to avoid injurious excess: hence a nut which feeds the drill is encircled by
a friction-strap in which it merely slips round without advancing the cutter
when the proper pressure is exceeded. There must be means of throwing
this into or out of gear, or advancing the tool in the work and of withdrawing
it—hence the handles seen attached to the brake-straps. Water must
be drawn from some convenient source, and caused to pass down the drill-tube—hence
the force-pump seen in the lowest part of the figure. The
rods must be raised by steam power and lowered by mechanism under
perfect control—hence suitable gearing is provided for that purpose.
The reader may be interested in learning what is the cost of “prospecting”
with this unique machinery. The company usually undertake to
bore the first 100 ft. for £40, but the next 100 ft. cost £80–-that is, for
200 ft. £120 would be charged; the third 100 ft. would cost £120–-that is
to say, the first 300 ft. would cost £240, and so on—each lower 100 ft. costing
£40 more than the 100 ft. above it. Some of the holes bored have
been of very great depth, and have been executed in a marvellously short
space of time. Thus, in 54 days, a depth of 902 ft. was reached at Girrick
in a boring for ironstone; another for coal at Beeston reached 1,008 ft.;
and at Walluff in Sweden 304½ ft. were put down in one week!
These machines are peculiarly suitable for submarine boring, for they
work as well under water as in the air; and they will no doubt be put into
requisition in the preliminary experiments about to be made for that great
project which bids fair to become a sober fact—the Channel Tunnel between
England and France; and as, by the time these pages will be before
the public, the work of the greatest and boldest rock-boring yet attempted
will have commenced, and the scheme itself will be the theme of every
tongue, the Author feels that the present article would be incomplete without
some particulars of the great enterprise. [1875.]
The notion of connecting England and France by a submarine line of
railways is not of the latest novelty, but has been from time to time
mooted by the engineers of both countries. The most carefully prepared
scheme, however, is embodied in the joint propositions of Sir J. Hawkshaw
365and Messrs. Brunlees and Low among English engineers; and those of
M. Gamond on the French side, which these gentlemen have prepared at
the invitation of the promoters of the scheme, give the clearest and most
authentic account of the considerations on which this gigantic enterprise
will be based, and from this document we draw the following passages:
The undersigned engineers, some of whom have been engaged for a
series of years in investigating the subject of a tunnel between France and
England, having attentively considered those investigations and the facts
which they have developed, beg to report thereon jointly for the information
of the committee.
These investigations supported the theory that the Straits of Dover were
not opened by a sudden disruption of the earth at that point, but had been
produced naturally and slowly by the gradual washing away of the upper
chalk; that the geological formations beneath the Straits remained in the
original order of their deposit, and were identical with the formations of the
two shores, and were, in fact, the continuation of those formations.
Mr. Low proposed to dispense entirely with shafts in the sea, and to commence
the work by sinking pits on each shore, driving thence, in the first
place, two small parallel driftways or galleries from each country, connected
at intervals by transverse driftways. By this means the air could be made
to circulate as in ordinary coal-mines, and the ventilation be kept perfect
at the face of the workings.
Mr. Low laid his plans before the Emperor of the French in April, 1867,
and in accordance with the desire of his Majesty, a committee of French
and English gentlemen was formed in furtherance of the project.
For some years past Mr. Hawkshaw’s attention has been directed to
this subject, and ultimately he was led to test the question, and to ascertain
by elaborate investigations whether a submarine tunnel to unite the railways
of Great Britain with those of France and the Continent of Europe
was practicable.
Accordingly, at the beginning of the year 1866, a boring was commenced
at St. Margaret’s Bay, near the South Foreland; and in March, 1866, another
boring was commenced on the French coast, at a point about three
miles westward of Calais; and simultaneously with these borings an examination
was carried on of that portion of the bottom of the Channel lying
between the chalk cliffs on each shore.
The principal practical and useful results that the borings have determined
are that on the proposed line of the tunnel the depth of the chalk
on the English coast is 470 ft. below high water, consisting of 175 ft. of
upper or white chalk and 295 ft. of lower or grey chalk; and that on the
French coast the depth of the chalk is 750 ft. below high water, consisting
of 270 ft. of upper or white chalk and 480 ft. of lower or grey chalk; and
that the position of the chalk on the bed of the Channel, ascertained from
the examination, nearly corresponds with that which the geological inquiry
elicited.
In respect to the execution of the work itself, we consider it proper to
drive preliminary driftways or headings under the Channel, the ventilation
of which would be accomplished by some of the usual modes adopted in
the best coal-mines.
As respects the work itself, the tunnel might be of the ordinary form, and
sufficiently large for two lines of railway, and to admit of being worked
by locomotive engines, and artificial ventilation could be applied; or it
366might be deemed advisable, on subsequent consideration, to adopt two
single lines of tunnel. The desirability of adopting other modes of traction
may be left for future consideration.
Such are the essential passages of the report which, in 1868, was submitted
to the Government of the Emperor Louis Napoleon, and was made
the subject of a special commission appointed by the Emperor to inquire
into the subject in all its bearings. The commission presented its report
in 1869, and these are the chief conclusions contained in it:
I. The commission, after having considered the documents relative to
the geology of the Straits, which agree in establishing the continuity, homogeneity,
and regularity of level of the grey chalk between the two shores
of the Channel,
Are of opinion that driving a submarine tunnel in the lower part of this
chalk is an undertaking which presents reasonable chances of success.
Nevertheless they would not hide from themselves the fact that its execution
is subject to contingencies which may render success impossible.
II. These contingencies maybe included under two heads: either in
meeting with ground particularly treacherous—a circumstance which the
known character of the grey chalk renders improbable; or in an influx of
water in a quantity too great to be mastered, and which might find its way
in either by infiltration along the plane of the beds, or through cracks
crossing the body of the chalk.
Apart from these contingencies, the work of excavation in a soft rock like
grey chalk appears to be relatively easy and rapid; and the execution of a
tunnel, under the conditions of the project, is but a matter of time and
money.
III. In the actual state of things, and the preparatory investigations
being too incomplete to serve as a basis of calculation, the commission will
not fix on any figure of expense or the probable time which the execution
of the permanent works would require.
The chart, Fig. 185, and the section, Fig. 186, will give an idea of the
course of the proposed tunnel, which will connect the two countries almost
at the nearest points. The depth of the water in the Channel along the
proposed line nowhere exceeds 180 ft.—little more than half the height of
St. Paul’s Cathedral, which building would, therefore, if sunk in the midst
of the Channel, still form a conspicuous object rising far above the waves.
But the tunnel will pass through strata at least 200 ft. below the bottom of
the Channel, rising towards each end with a moderate gradient; and from
the lower points of these inclines the tunnel will rise slightly with a slope
of 1 in 2,640 to the centre, or just sufficient for the purposes of drainage.
On the completion of the tunnel a double line of rails will be laid down in
it, and trains will run direct from Dover to Calais. Companies have already
been formed in England under the presidency of Lord Richard Grosvenor,
and in France under that of M. Michel Chevalier, and the legislation of
each country has sanctioned the enterprise. Verily the real magician of
our times is the engineer, who, by virtually abolishing space, time, and
tide, is able to transport us hither and thither, not merely one or two—almost
like the magicians we read of in the “Arabian Nights,” with their
enchanted horses or wonderful carpets—but by hundreds and by tens of
hundreds.
367
Fig. 185.—Chart of the Channel Tunnel.
The “Daily News” of January 22nd, 1875, in presenting its readers with
a chart of the proposed tunnel, offered also the following sensible and
interesting comment on the subject:
“This long-debated project has at length emerged from the region of
368speculation, and is entering the stage of practical
experiment. On this side the Channel a company
has been formed to carry out the work, and on the
other side the French Minister of Public Works
has presented to the Assembly a Bill authorizing a
French company to co-operate with the English engineers.
The enterprise is one worthy of the nations
which have in the present generation joined the two
shores of the Atlantic by an electric cable, and cut a
ship canal through the Isthmus of Suez, and of the
age which has obliterated the old barrier of the Alps.
All these gigantic undertakings seemed almost as
bold in conception and as difficult of execution as the
great work now about to commence. Those twenty
miles of sea have long been crossed by telegraph
lines; they will soon be bridged, as it were, by
splendid steamers; but even our own generation,
accustomed as it is to gigantic engineering works,
has scarcely regarded the construction of a railway
underneath the waves as within the reach of possibility.
M. Thomé de Gamond, who first made the
suggestion five and thirty years ago, was long regarded
as an over-sanguine person, who did not
recognize the inevitable limits of human skill and
power. A tunnel under twenty miles of stormy sea
seemed very much like an engineer’s dream, and it
is only within the last few years that it has been
regarded as a feasible project. Of its possibility,
however, there seems now to be no manner of doubt.
It is merely a stream of sea-water, and not a fissure
in the earth, which divides us from the Continent.
Prince Metternich was right in speaking of it as a
ditch. The depth is nowhere greater than one hundred
and eighty feet; and so far as careful soundings
can ascertain the condition of the soil underneath
the water, it consists of a smooth unbroken bed of
chalk. The success of the experiment depends on this
bed of chalk being continuous and whole. Should
any very deep fissure exist, which is extremely improbable,
the tunnel may probably not be driven
through it. But given, what every indication shows
to exist, a homogeneous chalk bed some hundreds
of feet in thickness, the driving of a huge bore for
twenty miles through it is a mere question of time,
money, and organization, and as the engineers have
these resources at their command, they are sanguine,
and we may even say confident, of success.
Fig. 186.—Section of the Channel Tunnel.
Fig. 187.—View of Dover.
“The method by which it is proposed that the
excavation shall be made is in some respects similar
to that which was successfully employed in
tunnelling the Alps. Mont Cenis was pierced by
machinery adapted to the cutting of hard rock;
the chalk strata under the Channel are to be bored
369by an engine, invented by Mr. Dickenson Brunton, which works in the
comparatively soft strata like a carpenter’s auger. A beginning will be
made simultaneously on both sides of the Channel, and the effort will at
first be limited to what we may describe as making a clear hole through
from end to end. This small bore, or driftway as it is called, will be some
seven or nine feet in diameter. If such a communication can be successfully
made, the enlargement will be comparatively easy. Mr. Brunton’s
machine is said to cut through the chalk at the rate of a yard an hour. We
believe that those which were used in the Mont Cenis Tunnel cut less than
a yard a day of the hard rock of the mountain. Two years, therefore,
ought to be sufficient to allow the workers from one end to shake hands
with those from the other side. The enlargement of the driftway into the
completed tunnel would take four years’ more labour and as many millions
of money. The millions, however, will easily be raised if the driftway is
made, since the victory will be won as soon as the two headways meet
under the sea. One of the great difficulties of the work is shared with the
Mont Cenis Tunnel, the other is peculiar to the present undertaking. The
Alps above the one, and the sea above the other, necessarily prevent the
use of shafts. The work must be carried on from each end; and all the
débris excavated must be brought back the whole length of the boring, and
all the air to be breathed by the workmen must be forced in. The provision
of a fit atmosphere is a mere matter of detail. In the great Italian
tunnel the machines were moved by compressed air, which, being liberated
when it had done its work, supplied the lungs of the workers with fresh
370oxygen. The Alpine engineers, however, started from the level of the
earth: the main difficulty of the Submarine Tunnel seems to be that it
must have as its starting-point at each end the bottom of a huge well
more than a hundred yards in depth. The Thames Tunnel, it will be remembered,
was approached, in the days when it was a show place, by a
similar shaft, though of comparatively insignificant depth. This enterprise
may indeed be said to bear something like the relation to the engineering
and mechanical skill of the present day which Brunel’s great undertaking
bore to the powers of an age which looked on the Thames Tunnel as the
eighth wonder of the world. Probably the danger which will be incurred
in realizing the larger scheme is less than that which Brunel’s workmen
faced.
“It is, of course, impossible for any estimate to be formed of the risks
of this enormous work. They have been reduced to a minimum by the
mechanical appliances now at our disposal, but they are necessarily considerable.
The tunnel is to run, as we understand, in the lower chalk, and
there will be, as M. de Lesseps told the French Academy, some fifty yards
of soil—a solid bed of chalk, it is hoped—between the sea-water and the
crown of the arch. Moreover, an experimental half-mile is to be undertaken
on each side before the work is finally begun; the engineers, in fact,
will not start on the journey till they have made a fair trial of the way.
Altogether the beginning seems to us to be about to be made with a combination
of caution and boldness which deserves success, even though it
should be unable to command it. Unforeseen difficulties may arise to
thwart the plans, but the enterprise, so far, is full of promise. The opening
of such a communication between this country and the Continent will
be a pure gain to the commercial and social interests on both sides. It
obliterates the Channel so far as it hinders direct communication, yet keeps
it intact for all those advantages of severance from the political complications
of the Continent, which no generation has more thoroughly appreciated
than our own. The commercial advantages of the communication
must necessarily be beyond all calculation. A link between the two chief
capitals of Western Europe, which should annex our railway system to the
whole of the railways of the Continent, would practically widen the world
to pleasure and travel and every kind of enterprise. The 300,000 travellers
who cross the Channel every year would probably become three millions
if the sea were practically taken out of the way by a safe and quick communication
under it. The journey to Paris would be very little more than
that from London to Liverpool. It is, however, quite needless to enlarge
on these advantages. The Channel Tunnel is the crowning enterprise of
an age of vast engineering works. Its accomplishment is to be desired
from every point of view, and, should it be successful, it will be as beneficent
in its results as the other great triumphs of the science of our time.”
The Channel Tunnel is not yet a fait accompli, although the preliminary
trial works have been made at both ends. Drift-ways of some
ten feet diameter have been cut beneath the waters of the strait, and
instead of the experimental half mile mentioned in the foregoing paragraph,
the works have been pushed forward on the English side for about
a mile and a quarter with complete success. As was anticipated, no
physical difficulties were met with, for the machines did their work with
the greatest ease, and the drift has now remained for some years practically
free from any infiltration of water. These results indicate that the
scheme might be completed with speed and safety. Parliament, however,
371has refused to allow the undertaking to proceed, being moved to
this course by the opinions of military authorities, who see dangers to
England in the completion of this enterprise, or at least such a disturbance
of the British complacency at the notion that our island might be
reached otherwise than “by the inviolate sea,” that the whole land would
be liable to terrors and alarms from invasion by stratagem. It is represented
that huge fortresses and a special army for that purpose would
become necessary to guard the mouth of the tunnel were it made. This
is, perhaps, the kind of objection which such an enterprise could not fail
to raise. But it can hardly be expected that all the commercial and
international advantages which the realization of the scheme would
undoubtedly secure are for ever to stand in abeyance for such opinions
as have, for the present, caused the operations to be suspended. It has
been pointed out that there are many ways of instantly rendering such
a tunnel impracticable in case of a sudden alarm. But the necessity
could only arise after a supposed paralysis or destruction of such army
and navy as Britain could bring together to defend her land. Perhaps
military skill will presently devise less costly methods of defence than
those authorities now suppose the tunnel would require; or, even if such
armaments were really necessary for our sense of insular security, the
expense might be no unprofitable outlay for the advantages to be gained.
It is satisfactory to know that the promoters of the scheme are sanguine
of the subsidence of the military and political prejudices, which are now
the only obstacles to its accomplishment. A somewhat unexpected
result from the operations in connection with the experimental driftways
has been the discovery, on the Kentish coast, of seams of coal underlying
the chalk at a workable depth.
Since the completion of the Mont Cenis Tunnel, a still greater piece
of rock boring has been begun and finished in the great tunnel of the
St. Gothard Railway. The construction of a railway to connect Italy
with Switzerland, was a project conceived as far back as 1838, when the
first railway company in the latter country was constructed. The route
of the proposed line was a matter of much debate, not alone on account
of difference of engineering opinions, but also by reason of the various
competing interests that would have to be reconciled and induced to
co-operate in the work. The St. Gothard route was only one of the
several schemes that were advocated, and the first decisive step appears
to have been taken at Lucerne, where, in 1853, a meeting was called by
the authorities of the canton to consider the merits of the project; the
result being that the Lucerne Government addressed to the Federal
Council a representation of the advantages this route would afford. More
discussion ensued, and it was only when Switzerland appeared likely to
have no share in the traffic between the Milan district and the more
northern parts of Europe that, in 1861, the partizans of the St. Gothard
route appointed a provisional committee to take action in the matter.
This committee had plans prepared, and sent a deputation to obtain the
assent of the Italian Government. The canton of Tessin, through which
373the projected line, or its then surviving rival, was designed to pass,
became a lively scene in the game of speculation, for promoters rushed
in to secure, if possible, concessions which they might sell at a very
advanced price to the winning party. For this purpose came to that
poor Swiss canton Jews and Christians from every land. The St. Gothard
route gained the day, and a Union was, in 1863, formed by the concurrence
of the two principal Swiss railways and fifteen of the cantons most
interested in the scheme. Difficulties and delays were, however,
encountered before the necessary compacts could be concluded with the
neighbouring states—and then there came the war of 1867. So that it
was not until the latter part of 1872 that the construction of the line was
actually entered upon. Before the great work of piercing the St. Gothard
had been completed, the undertaking was embarrassed by financial
difficulties arising from the fact of the lines on the Italian side costing
more than double the estimated amount. The Swiss Government, however,
voted a special subsidy, and the work, which had been suspended
for a while, was proceeded with; much attention being paid to its
economical prosecution. In 1881, when the line was opened, the mails
were carried between Zurich and Bellinzona in seven hours, instead of in
thirty hours as previously required for transit by the excellently appointed
mail carriages under the Federal Administration.
Fig. 187a.—Map of the St. Gothard Railway.
Besides the great tunnel, the St. Gothard line has some unique devices
in railway construction which cannot fail to interest the reader. Several
of the passes over the Alps have been made use of from time immemorial.
We know that Hannibal led his Carthaginian hosts over one
of them, and that they have been traversed by Roman legions, as well
as by Germanic hordes. But, although the St. Gothard is the most
direct of all the routes, it never afforded a passage to armies
or migratory tribes. The road through this pass was not formed by
the use of any elaborate appliances for overcoming the natural obstacles:
it was rather the work of simple peasants and mountain shepherds, with
such rough constructions in wood as might give a sufficiently secure
passage across the torrents and gorges. The old road keeps beside the
Reuss from the head of the lake of Lucerne until it reaches the highest
level of the pass, where the water-shed occurs. It then descends steeply,
with many twists and windings, to the banks of the Ticino, and it follows
the course of this river to its embouchure at Tresa, on Lago Maggiore.
The railway follows the same course, except that it cuts off the higher
part of the pass by the great tunnel piercing the mountain. The scenery
throughout could, perhaps, be nowhere equalled for the variety of its wild
grandeur.
The great tunnel of the St. Gothard passes from Gœschenen, on the
Reuss, beneath the col of the pass, and emerges close to the village of
Airolo, on the banks of the Ticino. The length of this tunnel is rather
more than nine and a quarter miles, so that it is about one and a half
miles longer than the Mont Cenis Tunnel. Its northern end is 3,638 feet
above the sea level; its southern end is higher, namely, 3,756 feet; but
there is an intermediate point in the tunnel higher than either-–3,786
feet—and from this there is a uniform incline in each direction. The
tunnel is 300 yards beneath the lowest part of the valley of Andermatt,
and the summits of the mountains it traverses are at least a mile above it.
The motive power by which the rock-drilling machines used in driving
the tunnel were actuated was, as in the case of the Mont Cenis Tunnel,
374compressed air; and the power used for compressing the air was, in this
case also, a head of water,—but this was not applied in the same way.
The waters of the Reuss at the northern side, and those of the Tremola
and of the Ticino at the southern side, were taken at a considerable height
in very large cast-iron pipes, and were made to act upon powerful turbines
that gave motion to the compressing machines. These were capable of
compressing the air so that its volume was reduced to one-twentieth, and
the pressure it then exercised would, of course, be equal to that of twenty
atmospheres, or about 300 lbs. on the square inch,—or more than three
times as much as was made use of in the Mont Cenis Tunnel. The compressed
air, carried through pipes to the head of the workings in the rock,
was there allowed to exert its force on the pistons of the perforators in the
manner already described. There was, in fact, a continual repetition of
exactly the same cycle of operations of boring, charging, firing, etc., that
are mentioned on page 355. A large quantity of the compressed air was
always allowed to rush into the work immediately after each blasting, in
order that the smoke and other products might be driven out and the
atmosphere rendered fit for respiration. In attacking the mountain simultaneously
from each side it was, of course, essential that the tunnels
should be driven in precisely the same direction, and therefore the positions
of the points of departure had to be determined by very careful
surveys. At Gœschenen, the gorge of the Reuss did not naturally admit
of a sufficient distance of vision to fix the direction with the required
accuracy, and it became necessary to pierce a thick mass of rock with a
special tunnel for the purpose of taking a sight sufficiently far back. At
Airolo, again, the tunnel had to enter the valley by curving towards the
village; and here a provisional gallery had to be driven in the straight line.
PLATE XVI.
THE NORTH MOUTH OF THE GREAT TUNNEL, ST. GOTHARD RAILWAY.
Several contractors competed for the work of constructing this great
tunnel, and it was at first supposed that an Italian company, which was
managed by some of the principal engineers engaged on the Mont
Cenis, would be almost certain to obtain the contract. The promoters,
however, intrusted the work to a private individual, M. Louis Favre, of
Geneva. This gentleman undertook to complete the tunnel in eight
years, at the price of 2,800 francs per mètre for the work of excavation
merely, exclusive of masonry, etc. This cost would be not far from £101
per English yard. The contract was signed on August 7th, 1872, and on
September 12th of the same year M. Favre commenced operations at the
southern end, and the work at the northern end was begun on October 9th
following. The operations were carried on with great energy, and even
during the period of the Company’s financial difficulties there was no
stoppage of the works between Gœschenen and Airolo. It has been
suggested that it was largely due to the regular and successful progress of
this great piece of rock boring that the Company were enabled to re-establish
themselves on a basis that ensured the completion of the whole
undertaking. The contractor, on his part, did not fail to encounter many
physical difficulties. At the southern end much trouble was caused by
torrents of water gushing from the soil, many of these being of great
volume and force; in fact, the work was here carried on for nearly a
whole year in the midst of water—for the ground for the first mile consisted
of glacial and other deposits, which were intersected by subterranean
water-courses. Reaching the solid rock was here a relief. But at
Gœschenen little of loose formation was met with; but the rock encountered
was of extreme hardness—consisting, indeed, of almost pure
375quartz, which had the effect
of quickly blunting the points
of even the best tempered
tools. But another kind of
difficulty had to be overcome
when the workings got beneath
the vale of Urseren.
Here, at several places, layers
of argillaceous matter were
found between the masses of
hard rock. These layers
were easy enough to pierce
through, but on account of
the pressure of the rocks in
which they were interspersed,
they were squeezed out and
gradually protruded within
the tunnel, which would soon
have become entirely obstructed.
At first a very
massive lining of timber was
tried, but it was soon found
that this must be replaced by
a solid vaulting of stone.
The first vault failed to sustain
the pressure, and so did
the second, although the
thickness of the material was
more than a yard. In some
places these operations had
to be several times repeated,
and from this cause the cost
of parts of the tunnel has
been nearly £1,000 per yard.
Fig. 187b.—The Uppermost Bridge over the Maïenreuss.
The instances above mentioned
may be taken as mere
specimens of the physical
difficulties attending a work
of this kind. There are often
others arising from the unusual
circumstances under
which the workmen are
placed, and others again from
accidental causes alone. M.
Favre experienced some of
these, as, for example, when
one year a fire destroyed the
greater part of the village of
Airolo; another year there
was a strike on the part of
the workmen. The high
temperature in the workings
was, especially towards the
376end, a source of great trouble. The cause of the heat is no doubt
the same as that which is held to support the theory of the earth’s
central heat. Numberless observations have established the fact that the
temperature of the earth’s crust increases as we go deeper. The
increase appears not to be uniform in different places—at least there
is much discrepancy in the estimates that have been made. But as
a sufficient approximation to a general statement, it may be taken as
proved that for every seventy feet or so that you go below the surface
of the ground, there is an increase of the temperature of the strata equal
to 1° Fahrenheit. Now, the workmen in the two sections of the tunnel
had, at last, to carry on their labour in a temperature of more than 100°
Fahrenheit. This, perhaps, might have been one cause of some unprecedented
kinds of malady that appeared amongst the tunnel labourers.
M. Favre himself was not destined to witness the completion of his great
undertaking, for, on July 19th, 1879, as he was returning from an
inspection of the tunnel, he fell into the arms of his companions, struck
down by a fatal attack of apoplexy. On February 29th, 1880, the
last fuse required to blast down the rock separating the two tunnels was
fired by one of the few workmen who had been engaged in the operations
during the whole period from their commencement. It was found that
the two tunnels met exactly and coincided in direction.
Fig. 187c.—The Bridges over the Maïenreuss near Wasen.
The construction of such a line of railway as the St. Gothard tries the
skill of the engineer, and taxes all the resources of his art. The problems
presented by the nature of the route, and the requirements of the iron
road, have in this case been successfully solved by bold expedients—by
new and ingenious devices. The reader will readily understand that the
ordinary cart road may wander about, so to speak, of its own will; it is
not confined to the limited gradient of the line; or obliged to make its
turns and curves of at least a certain radius. Now, there are portions of
the valley where the general slope is too steep for the railway to follow,
and where it was necessary to form it in zig-zags, so that certain sections
of the gorge or valley may be several times traversed by the line
returning upon itself. Fig. 187d is a view showing an incident of this kind,
and one of the most interesting spots on the route. The dark line on the
spectator’s right is the track of the railway; the white trace, which in the
lower part of the view is seen on the other side of the Reuss, is the
ordinary road. If this last be followed up the valley, it will be seen to
cross first the Reuss, and then a tributary stream (the Maïenreuss)
descending through a gorge on the right, after which it zig-zags up a hill
to the village of Wasen (the church of which village is seen crowning the
eminence in the centre of our view), and then it continues its course up
the valley, passing through a small village, and disappearing over the
shoulder of a hill on the right bank of the river. Let us now carefully
follow the railway from where the train at the bottom of the picture is
seen ascending the gradient. The line presently passes under a bridge,
and then enters the tunnel, near to the entrance of which a small building
will be noticed. The course of the tunnel is shown by the curve marked
in dots, for this tunnel makes a round within the rock, and the railway
emerges to day again at a point lower down in the course of the valley
than at the entrance to the tunnel, but at a higher level. It is seen in
the figure appearing from behind the rocks in the right-hand lower
corner, passing under a short tunnel and continuing along the mountain
side. The curved tunnel resembles in direction part of the turn of a
379corkscrew; it is one of a series of helicoidal tunnels of which there are
several examples on the line. The entrance to this tunnel is 2,539 feet, the
exit 2,654 feet, above the sea level. It is known as Pfaffensprung (Monk’s
Leap) Tunnel. The line again enters a short tunnel, and immediately
crosses the deep gorge of the Maïenreuss, to plunge again into another
tunnel at the base of this hill on which Wasen stands. Higher up it
crosses the Reuss and enters the helicoidal tunnel of Wattingen (dotted
line). On emerging from this, the line re-crosses the Reuss, and may
now be traced down the valley, but higher up on the mountain side,
coming in the reverse direction, and after passing Wasen on the other
side, re-crossing the Maïenreuss gorge by a second bridge. Then turning
back again through another helicoidal tunnel (Leggistein) the line crosses
the Maïenreuss for the third time, and continues its course up the valley.
Fig. 187c gives us a near view of Wasen, and a glimpse up the gorge of the
Maïenreuss from its junction with the Reuss. The bridge with the large
single arch is that which carries the ordinary road, and higher up we see
the three iron bridges that carry the railway backwards and forwards in
its doublings. We can well imagine the perplexity of anyone ascending
the valley in the train for the first time, and ignorant of the peculiarities
of this extraordinary railway. In crossing the first, or lowest bridge, over
the Maïenreuss, he would catch a glimpse of the church of Wasen, perched
on its hill, high above him, and on his right. After being carried through
more tunnels, and over more bridges, he would some minutes afterwards
be disposed to think that his eyes were deceiving him, for there, still on
his right, he would see the same church, but now on about the same level
as the train. Again, after more tunnels and bridges, the church would
once more appear, transferred to the left of the line, and sunk very far
down. These several apparitions of the same building in different positions,
after the train has seemed to have been pursuing its onward course
the while,—which course would not be judged by any impressions the
traveller would usually receive to be other than rectilinear,—are indeed a
regular bewilderment to the inexperienced traveller. He is then obliged
finally to resign himself passively to be carried he knows not whither or
how, for his sense of direction is completely at fault;—the train comes
out of tunnels which seem turned the wrong way; the river, which he
expected to find on the left hand, he sees on the right; and the Reuss
appears to have reversed the direction of its flow.
Fig. 187d.—Windings of the Line near Wasen.
It is understood that the St. Gothard line has been a great commercial
success, for the number of passengers entering and leaving Italy by that
route has been enormous, and still shows a large annual increase.
Indeed, the prosperity of the line has been so great that the project has
been revived of carrying another railway over the Alps to connect Italy
and Switzerland by way of the Simplon. If this scheme should be carried
out, the mountains will be pierced by a tunnel of a length double that of
the St. Gothard.
380
Fig. 188.
LIGHT. — SOME PHENOMENA OF LIGHT. — VELOCITY OF LIGHT. — REFLECTION OF LIGHT. — REFRACTION. — DOUBLE REFRACTION AND POLARIZATION. — CAUSE OF LIGHT AND COLOUR.
The foregoing pages have been devoted to the description of inventions
or operations in which mechanical actions are the most obvious
features. Some of the contrivances described have for their end and object
the communication of motion to certain bodies, others the arrangement of
materials in some definite form, and all are essentially associated with the
idea of what is called matter. But we are now about to enter on another
region—a region of marvels where all is enchanted ground—a region in
which we seem to leave far behind us our grosser conceptions of matter,
and to attain to a sphere of more refined and subtile existence. For we
381are about to show some results of those beautiful investigations in which
modern science has penetrated the secrets of Nature by unfolding the
laws of light—
“Light
Ethereal, first of things, quintessence pure.”
The diversity and magnificence of the spectacles which, by day as well
as by night, are revealed to us by the agency of light, have been the theme
of the poet in every age and in every country. It cannot fail to arrest the
attention to find Science declaring that all the loveliness of the landscape,
the fresh green tints of early summer and the golden glow of autumn,
the brilliant dyes of flowers, of insects, of birds, the soft blue of the cloudless
sky, the rosy hues of sunset and of dawn, the chromatic splendour of
rubies, emeralds, and other gems, the beauties of the million-coloured
rainbow,—are all due to light—to light alone, and are not qualities of the
bodies themselves, which merely seem to possess the colours. The following
quaint stanzas, in which a poet of the seventeenth century addresses
“Light” have a literal correspondence with scientific truth:
“All the world’s bravery, that delights our eyes,
Is but thy several liveries;
Thou the rich dye on them bestowest,
Thy nimble pencil paints this landscape as thou goest.
“A crimson garment in the rose thou wearest:;
A crown of studded gold thou bearest;
The virgin lilies, in their white,
Are clad but with the lawn of almost naked light.
“The violet, Spring’s little infant, stands
Girt in thy purple swaddling-bands;
On the fair tulip thou dost dote;
Thou clothest it in a gay and parti-coloured coat.”
All these beauties are indeed derived from the imponderable and invisible
agent, light; and the variety and changefulness of the effects we may constantly
observe show that light possesses the power of impressing our visual
organs in a thousand different ways, modified by the surrounding circumstances,
as witness that ever-shifting transformation scene—the sky. In
the skies of such a climate as that of England there are ceaseless changes
and ever-beautiful effects, producing everywhere more perfect and diversified
pictures than the richest galleries can show. In the night how changed
is the spectacle, when the sun’s more powerful rays are succeeded by the soft
light of the moon, sailing through the azure star-bestudded vault! What
limitless scope for the artist is afforded by these innumerable modifications
of a single subtile agent, in light and shade, brightness and obscurity, in the
contrasts and harmonies of colours, and in the countless hues resulting from
their mixtures and blendings!
It will be necessary, before attempting to explain the discoveries and
inventions which prove how successfully science, aided by the powerful
mathematical analysis of modern times, has acquired a knowledge of the
ways of light, to discuss such of the ordinary phenomena as have a direct
bearing upon the subjects to be considered.
382
Fig. 189.—Rays.
It may be considered as a matter of common experience that light is
able to pass through certain bodies, such as air and gases, pure water,
glass, and a number of other liquids and solids, which, by virtue of this
passage of light, we term transparent, in opposition to another class of
bodies, called opaque, through which light does not pass. That light traverses
a vacuum may be held as proved by the light of the sun and stars
reaching us across the interplanetary spaces; but it may also be made the
subject of direct experiment by an apparatus described below, Fig. 190.
Another fact, very obvious from common observation, is that light usually
travels in straight lines. Some familiar experiences may be appealed to
for establishing this fact. For example, every one has observed that the
beams of sunlight which penetrate an apartment through any small opening
pursue their course in perfectly straight lines across the atmosphere, in
383which their path is rendered visible by the floating particles of dust. It is
by reason of the straightness with which rays of light pursue their course
that the joiner, by looking along the edge of a plank, can judge of its truth,
and that the engineer or surveyor is able by his theodolite and staff to set
out the work for rectilinear roads or railways. On a grander scale than in
the sunbeam traversing a room, we witness the same fact in the effect represented
in Fig. 189, where the sun, concealed from direct observation, is seen
to send through openings in the clouds, beams that reveal their paths by
lighting up the particles of haze or mist contained in the atmosphere. It
is not the air itself which is rendered visible; but whenever a beam of sunlight,
or of any other brilliant light, is allowed to pass through an apartment
which is otherwise kept dark, the track of the beam is always distinctly
visible, and, especially if the light be concentrated by a lens or concave
mirror, the fact is revealed that the air, which under ordinary circumstances
appears so pure and transparent, is in reality loaded with floating
particles, requiring only to be properly lighted up to show themselves.
Fig. 190.
Professor Tyndall, in the course of some remarkable researches on the
decomposition of vapours by light, wished to have such a glass tube as that
represented in Fig. 190, filled with air perfectly free from these floating particles.
When the beam of the electric lamp passed through the exhausted
tube, no trace of the existence of anything within the tube was revealed,
for it appeared merely like a black gap cut out of the visible rays that traversed
the air; thus proving that light, although the agent which makes all
things become visible, is itself invisible—that, in fact, we see not light, but
only illuminated substances. When, however, air was admitted to the tube,
even after passing through sulphuric acid, the beam of the light became
clearly revealed within the tube, and it was only by allowing the air to stream
very slowly into the exhausted glass tube through platinum pipes, packed
with platinum gauze and intensely heated, that Professor Tyndall succeeded
in obtaining air “optically empty,” that is, air in which no floating particles
revealed the track of the beams. The destruction of the floating matter
by the incandescent metal proves the particles to be organic; but a more
convenient method of obtaining air free from all suspended matter was
found by Professor Tyndall to be the passing of the air through a filter of
cotton wool. It must not be supposed that it is only occasionally, or in
dusty rooms, laboratories, or lecture-halls, that the air is charged with
organic and other particles—
“As thick as motes in the sunbeams.”
“The air of our London rooms,” says Tyndall, “is loaded with this
384organic dust, nor is the country air free from its pollution. However ordinary
daylight may permit it to disguise itself, a sufficiently powerful beam
causes the air in which the dust is suspended to appear as a semi-solid,
rather than as a gas. Nobody could, in the first instance, without repugnance,
place the mouth at the illuminated focus of the electric beam and
inhale the dust revealed there. Nor is this disgust abolished by the reflection
that, although we do not see the nastiness, we are drawing it in our
lungs every hour and minute of our lives. There is no respite to this contact
with dirt; and the wonder is, not that we should from time to time
suffer from its presence, but that so small a portion of it would appear to
be deadly to man.” The Professor then goes on to develop a very remarkable
theory, which attributes such diseases as cholera, scarlet fever,
small pox, and the like, to the inhalation of organic germs which may form
part of the floating particles. But we must return to our immediate subject
by a few words on the
Fig. 191.—Telescopic appearance of Jupiter and Satellites.
It may be stated at once, that this velocity has the amazing magnitude
of 185,000 miles in one second of time, and that the fact of light requiring
time to travel was first discovered, and the speed with which it
does travel was first estimated, about 200 years ago, by a Danish astronomer,
named Roemer, by observations on the eclipses of the satellites of
Jupiter. The satellites of Jupiter are four in number, and as they revolve
385nearly in plane of the planet’s orbit, they are subject to frequent eclipses
by entering the shadow cast by the planet; in fact, the three inner satellites
at every revolution. Fig. 191 represents the telescopic appearance of
the planet, from a drawing by Mr. De La Rue, and in this we see the well-known
“belts,” and two of the satellites, one of which is passing across the
face of the planet, on which its shadow falls, and is distinctly seen as a
round black spot, while the other may be noticed at the lower right-hand
corner of the cut. The satellite next the planet (Io) revolves round its
primary in about 42½ hours, and consequently it is eclipsed by plunging
into the shadow of Jupiter at intervals of 42½ hours, an occurrence which
must take place with the greatest regularity as regards the duration of the
intervals, and which can be calculated by known laws when the distance
of the satellite from the planet has been determined. Nevertheless, Roemer
observed that the actual intervals between the successive immersions of
Io in the shadow of Jupiter did not agree with the calculated period of
rotation when the distance between Jupiter and the earth was changing,
in consequence chiefly of the movement of the latter (for Jupiter requires
nearly twelve years to complete his revolution, and may, therefore,
be regarded as stationary as compared for a short time with the earth).
Roemer saw also, that when this distance was increasing, the observed
intervals between the successive eclipses were a little greater, and that
when the distance was decreasing they were a little less, than the calculated
period. And he found that, supposing the earth, being at the point of its
orbit nearest to Jupiter, to recede from that planet, the sum of all the retardations
of the eclipses which occur while the earth is travelling to the
farthest point of its orbit, amounts to 16½ minutes, as does also the sum of
the deficiencies in the period when the earth, approaching Jupiter, is passing
from the farthest to the nearest point of her orbit. While, however, the
earth is near the points in her orbit farthest from, or nearest to Jupiter, the
distance between the two planets is not materially changing between successive
eclipses, and then the observed intervals of the eclipses coincide,
with the period of the satellite’s rotation. The reader will, after a little
reflection, have no difficulty in perceiving that the 16½ minutes represent the
time which is required by the light to traverse the diameter of the earth’s
orbit; or, if he should have any difficulty, it may be removed by comparing
the case with the following.
Let us suppose that from a railway terminus trains are dispatched every
quarter of an hour, and that the trains proceed with a common and uniform
velocity of, say, one mile per minute. Now, a person who remains
stationary, at any point on the railway, observes the trains passing at
regular intervals of fifteen minutes, no matter at what part of the line
he may be placed. But now, let us imagine that a train having that very
instant passed him, he begins to walk along the line towards the place from
which the trains are dispatched: it is plain that he will meet the next train
before fifteen minutes—he would, in fact, meet it a mile higher up the line
than the point from which he began his walk fourteen minutes before; but
the train, taking a minute to pass over this mile, would pass his point of
departure just fifteen minutes after its predecessor. And our imaginary
pedestrian, supposing him to continue his journey at the same rate, would
meet train after train at intervals of fourteen minutes. Similarly, if he
walked away from the approaching trains, they would overtake him at
intervals of sixteen minutes. And again, it would be easy for him to calculate
the speed of the trains, knowing that they passed over each point of
386the line every fifteen minutes. Thus, suppose him to pass down the line a
distance known to be, say, a quarter of a mile; suppose he leaves his station
at noon, the moment a train has passed, and that he takes, say an
hour, to arrive at his new station a quarter of a mile lower; here, observing
a train to pass at fifteen seconds after one o’clock, and knowing
that it passed his original station at one, he has a direct measure of the
speed of the trains. Here we have been explaining a discovery two centuries
old; but our purpose is to prepare the reader for an account of how
the velocity of light has been recently measured in a direct manner, and
it certainly appears a marvellous achievement that means have been found
to measure a velocity so astounding, not in the spaces of the solar system,
or along the diameter of the earth’s orbit, but within the narrow limits of
an ordinary room! The reliance with which the results of these direct
measures will be received, will be greatly increased by the knowledge of
the astronomical facts with which they show an entire concordance. In
taking leave of Roemer, we may mention that his discovery, like many
others, and like some inventions which have been described in this book,
did not for some time find favour with even the scientific world, nor was
the truth generally accepted, until Bradley’s discovery of the aberration of
light completely confirmed it.
Fig. 192.
To two gifted and ingenious Frenchmen we are indebted for independent
measurements of the velocity of light by two different methods. The general
arrangement of M. Fizeau’s method is represented in Fig. 192, in which
the rays from a lamp, L, after passing through a system of lenses, fall upon
a small mirror, M N, formed of unsilvered plate-glass inclined at an angle of
45° to the direction of the rays; from this they are reflected along the axis of
a telescope, T, by the lens of which being rendered parallel, they become a
cylindrical beam, B, which passes in a straight line to a station, D, at a
distance of some miles (in the actual experiment the lamp was at Suresnes
and the other station at Montmartre, 5½ miles distant) whence the beam is
reflected along the same path, and returns to the little plate of glass at
M N, passing through which it reaches the eye of the observer at E. At W
is a toothed wheel, the teeth of which pass through the point F, where the
387rays from the lamp come to a focus; and as each tooth passes, the light is
stopped from issuing to the distant station. This wheel is capable of receiving
a regular and very rapid rotation from clockwork in the case, C,
provided with a register for recording the number of its revolutions. If the
wheel turns with such a speed that the light permitted to pass through
one of the spaces travels to the mirror and back in exactly the same time
that the wheel moves and brings the next space into the tube, or the second
space, or the third, or any space, the reflected light will reach the spectator’s
eye just as if the wheel were stationary; but if the speed be such that a
tooth is in the centre of the tube when the light returns from the mirror,
then it will be prevented from reaching the spectator’s eye at all, so long
as this particular speed is maintained, but either a decrease or an increase
of velocity would cause the luminous image to reappear. Speeds between
those by which the light is seen, and those by which it entirely disappears,
cause it to appear with merely diminished brilliancy. It is only necessary
to observe the speed of the wheel when the light is at its brightest, and when
it suffers complete eclipse, for then the time is known which is required
for space and tooth respectively to take the place of another space—and
hence the time required for the light to pass to the mirror and back is
found.
M. Foucault’s method is similar in principle to that used by Wheatstone
in the measurement of the velocity of electricity. He used a mirror which
was made to revolve at the rate of 700 or 800 turns per second, and the
arrangement of the apparatus was such as to admit of the measurement of
the time taken by light to pass over the short space of about four yards!
More recently, however, he has modified and improved his apparatus by
adopting a most ingenious plan of maintaining the speed of the mirror at
a determined rate, which he now prefers should be 400 turns per second,
while the light is reflected backwards and forwards several times, so that it
traverses a path of above 20 yards in length. The time taken by the light
to travel this short distance is, of course, extremely small, but it is accurately
measured by the clockwork mechanism, and found to be about the
1 150000000th of a second! The results of these experiments of Foucault’s
make the velocity of light several thousand miles per second less than that
deduced from the astronomical observation of Roemer and Bradley, in
which the distance of the earth from the sun formed the basis of the calculations;
and hence arose a surmise that this distance had been over-estimated.
That such had, indeed, been the case was confirmed almost immediately
afterwards by a discussion among the astronomers as to the
correctness of the accepted distance, the result of which has been that the
mean distance, which was formerly estimated at 95 millions of miles, has,
by careful astronomical observations and strict deductions, been now estimated
at between 91 and 92 millions of miles. The famous transit of Venus
December 9th, 1873–-to observe which the Governments of all the chief
nations of the world sent out expeditions—derived its astronomical and
scientific importance from its furnishing the means of calculating, with
greater correctness than had yet been attained, the distance of the earth
from the sun.
Fig. 193.
Fig. 194.
Fig. 195.
388
Long before plate glass backed by brilliant quicksilver ever reflected
the luxurious appointments of a drawing-room; long before looking-glass
ever formed the mediæval image of “ladye fair”; long before the
haughty dames of imperial Rome were aided in their toilettes by specula;
long before the dark-browed beauties of Egypt peered into their brazen
mirrors; long, in fact, before men knew how to make glass or to polish
metals, their attention and admiration must have often been riveted by
those perfect and inverted pictures of the landscape, with its rocks, trees,
and skies, which every quiet lake and every silent pool presents. Enjoyment
of the spectacle probably prompted its imitation by the formation artificially
of smooth flat reflecting surfaces; and no doubt great skill in the production
of these, and their application to purposes of utility, coquetry, and
luxury, preceded by many ages any attempt to discover the laws by which
light is reflected. The most fundamental of these laws are very simple, and
for the purpose we have in view, it is necessary that they should be borne
in mind. Let A B, Fig. 193, be a plane reflecting surface, such as the surface
of pure quicksilver or still water, or a polished surface of glass or metal,
and let a ray of light fall upon it in the direction, I O, meeting the surface at
O, it will be reflected along a line, O R,—such that if at the point O we draw
a line, O P, perpendicular to the surface, the incident ray, I O, and the reflected
ray, O R, will form equal angles with the perpendicular—in other
words, the angle of incidence will be equal to the angle of reflection, and
the perpendicular, the incident ray, and the reflected ray, will all be in
one plane perpendicular to the reflecting plane. It would be quite easy to
389prove from this law that the luminous rays from any object falling on a
plane reflecting surface are thrown back just as if they came from an
object placed behind the reflecting surface symmetrically to the real object.
The diagrams in Figs. 194 and 195 will render this clear. In the second
diagram, Fig. 195, it will be noticed that only the portion of the mirror between
Q and P takes any part in the action, and therefore it is not necessary,
in order to see objects in a plane mirror, that the mirror should be exactly
opposite to them; thus the portion O Q might be removed without the eye
losing any part of the image of the object A B.
Fig. 196.
There are many very interesting and important scientific instruments in
which the laws of reflection from plane surfaces are made use of—such, for
example, as the sextant and the goniometer; but passing over all these, we
may say a word about the formation of several images from one object by
using two mirrors. It has already been explained that the action of a plane
mirror is equivalent to the placing of objects behind it symmetrically disposed
to the real object. The reflections, or virtual images in the mirror,
behave optically exactly as if they were themselves real objects, and are reflected
by other mirrors in precisely the same manner. From this it follows
that two planes inclined to each other at an angle of 90° give three images
of an object placed between them, the images and the object apparently
placed at the four angles of a rectangle. When the mirrors are inclined to
each other at an angle of 60°, five images are produced, which, with the
original object, show an hexagonal arrangement. The formation of these by
the principle of symmetry is indicated in Fig. 196. It was these symmetrically
disposed images which suggested to Sir David Brewster the construction
of the instrument so well known as the kaleidoscope, in which two—or,
still better, three—mirrors of black glass, or of glass blackened on one side,
are placed in a pasteboard tube inclined to each other at 60°: one end of
the tube is closed by two parallel plates of glass; the outer one ground,
but the inner transparent, leaving between them an interval, in which are
placed fragments of variously-coloured glass, which every movement of
390the instrument arranges in new combinations. At the other end of the
tube is a small opening—on applying the eye to which one sees directly
the fragments of glass, with their images so reflected that beautifully
symmetrical patterns are produced; and this with endless variety. When
this instrument was first made in the cheap form in which it is now so
familiarly known, it obtained a popularity which has perhaps never been
equalled by any scientific toy, for it is said that no fewer than 200,000
kaleidoscopes were sold in London and Paris in one month.
Fig. 197.—Polemoscope.
By way of contrast to the mirrors of the kaleidoscope harmlessly producing
beautiful designs, by symmetrical images of fragments of coloured
glass, we show the reader, in Fig. 197, mirrors which are reflecting quite
other scenes, for here is seen the manner in which even the plane mirror
has been pressed into the service of the stern art of war. The mirrors are
employed, not like those of Archimedes, to send back the sunbeams from
every side, and by their concentration at one spot to set on fire the enemy’s
works, but to enable the artillerymen in a battery to observe the effect of
their shot, and the movement of their adversaries, without exposing themselves
to fire by looking over the parapet of their works. The contrivance
has received the appropriate name of Polemoscope (πολεμος, war, and σκοπεω,
391to view), and it consists simply, as shown in the figure, of two plane mirrors
so inclined and directed, that in the lower one is seen by reflection the localities
which it is desired to observe.
Fig. 198.—Apparatus for Ghost Illusion.
We return once more to the arts of peace, in noticing the advantage
which has been lately taken of plane mirrors for the production of spectral
and other illusions, in exhibitions and theatrical entertainments, the improvement
in the manufacture of plate-glass having permitted the production
of enormous sheets of that substance. Among the most popular exhibitions
of this class was that known as “Pepper’s Ghost,” the arrangement
of the mirrors having been the subject of a patent taken out by Mr. Pepper
and Mr. Dircks jointly. The principle on which the production of the
illusion depends, may be explained by the familiar experience of everybody
who has noticed that, in the twilight, the glass of a window presents to a
person inside of a room the images of the light or bright objects in the
apartment, while the objects outside are also visible through the glass.
As, by night coming on, the reflections increase in brilliancy, the darkness
outside is almost equivalent to a coat of black paint on the exterior surface
of the glass; but, on the contrary, in the daylight no reflection of the interior
of the room is visible to the spectator inside, on looking towards the
window. The reflections are present, nevertheless, in the day-time as well
as at night, only they are overpowered and lost when the rays which reach
the eye through the glass are relatively much more powerful. Even in the
day-time the image of a lighted candle is usually visible, in the absence of
392direct sunshine, against a dark portion of the exterior objects as a back-ground.
The visibility, or otherwise, of the internal objects by reflection, and
of the external objects seen through the glass, depends entirely on the relative
intensities of the illumination, for the more illuminated side overpowers
and conceals the other, just as the rising sun causes the stars “to pale their
ineffectual fires.” Hence, on looking through the window on a dark night,
we cannot see objects out of doors unless we screen off the reflection of the
illuminated objects in the room. If the rays transmitted through the glass,
and those which are reflected, have intensities not very different, we see
then the reflected images mixed up in the most curious manner with the
real objects. It is exactly in this way that the ghosts are made to appear
in the illusion of which we are speaking. The real actors are seen through
a large plate of colourless and transparent glass, and from the front surface
of this glass rays are reflected which apparently proceed from a phantom
taking a part in the scene among the real actors. The arrangement is
shown in Fig. 198, where E G is the stage, separated from the auditorium,
h, by a large plate of transparent glass, E F, placed in an inclined position,
and not visible to the spectators, for the lights in front are turned down,
and the stage is also kept comparatively dark. Parallel to the large plate
of glass is a silvered mirror, C D, placed out of the spectators’ sight, and
receiving the rays from a person at A, also out of sight of the spectators,
and strongly illuminated by an oxy-hydrogen lime-light at B. The manner
in which the rays are reflected from the silvered mirror to the plate-glass,
and hence reflected so as to reach the spectators and give them the impression
of a figure standing on the stage at G, is sufficiently indicated by
the lines drawn in the diagram. The apparitional and unsubstantial character
of the image is derived from its seeming transparency, and from
the manner in which it may be made to melt away, by diminishing the
brightness of the light which falls on the real person. The introduction of
the second mirror was a great improvement, for by this the phantom is
made to appear erect, while its original stands in a natural attitude. Whereas,
with only the plate-glass, E F, the ghost could not be made to appear
upright, unless, indeed, as was sometimes done, the plate was inclined at
an angle of 45°, and the actor of the ghost lay horizontally beneath it. A
scene of the kind produced by the improved apparatus, is represented in
Fig. 198a.
Fig. 198a.—The Ghost Illusion.
Another illusion is produced by the help of a large silvered mirror,
placed at an inclination of 45°, sloping backwards from the floor, and,
in consequence, presenting to the spectators the image of the ceiling,
which appears to them the back of the scene. The mirror is perforated
near the centre by an opening, through which a person passes his head,
and, all his body being concealed by the mirror, the effect produced is that
of a head floating in the air. Means are provided of withdrawing the
mirror, when necessary, while the curtain is down, and then the real back
of the scene appears, which, of course, is exactly similar to the false one
painted on the ceiling. Fig. 199 represents a scene produced at the Polytechnic
by a somewhat similar arrangement of mirrors, under the management
of Mr. Pepper. Plane mirrors were employed in another piece of
natural magic which this gentleman exhibited to the public, who were
shown a kind of large box, or cabinet, raised from the floor, and placed
in the middle of the stage, so that the spectators might see under it and
all round it. Inside of the box were two silvered mirrors the full height of
it, and these were hinged to the farther angles, so that each one being
394folded with its face against a side of the box, their backs formed the apparent
sides, and were painted exactly the same as the real interior of the
box. When the performer enters the box, the door is closed for an instant,
while he, stepping to the back, turns the mirrors on their hinges until their
front edges meet, where an upright post in the middle of the box conceals
their line of junction. The performer thus places himself behind the
mirrors in the triangular space between them and the back of the box,
while the mirrors, now inclined at angles of 45° to the sides, reflect
images of these to the spectators when the door is opened, and the spectators
see then the box apparently empty, for the reflection of the sides
appears to them as the back of the cabinet. The entertainment was sometimes
varied by a skeleton appearing, on the door being opened, in the place
of the person who entered the cabinet. It is hardly necessary to say that
the skeleton was previously placed in the angle between the mirrors where
the performer conceals himself.
Fig. 199.—Illusion produced by Mirrors.
395
Fig. 200.—A Stage Illusion.
To the same inventive gentleman, whose ingenious use of plane mirrors
has thus largely increased the resources of the public entertainer, is due
another stage illusion, the effect of which is represented in Fig. 200; and,
although it does not depend on reflection, it may be introduced here as showing
how the perfection of the manufacture of plate-glass, which makes it
available for the ghost exhibition, can be applied in another way in dramatic
spectacles. The female form, here supposed to be seen in a dream by the
sleeper, is not a reflection, although she appears floating in mid-air, strangely
detached from all supports, but the real actress. This is accomplished by
making use of the transparency of plate-glass, a material strong enough to
afford the necessary support, and yet invisible under the circumstances of
the exhibition.
But it is not behind the turned-down footlights, or in the exhibitions of
the showman, that we find the most beautiful illustrations of the laws of
reflection. In the quiet mountain mere, amid the sweet freshness of nature,
we may often see tree, and crag, and cliff, so faithfully reproduced, that it
396needs an effort of the understanding to determine where substance leaves
off and shadow begins, a condition of the liquid surface indicated in two
lines by Wordsworth:
“The swan, on still St. Mary’s Lake,
Floats double, swan and shadow.”
The landscape painter is always gratified if he can introduce into his
picture some piece of water, and it can hardly be doubted that much of the
charm of lakes and rivers is due to their power of reflecting. Look on
Fig. 201, a view of some buildings at Venice; and, in order to see how much
of its beauty is owing to the quivering reflections, imagine the impression
it would produce were the place of the water occupied by asphalte pavement,
or a grass lawn. The condition of the reflections here represented
is perhaps even more pleasing than that produced by perfect repose: they
are in movement, and yet not broken and confused:
“In bright uncertainty they lie,
Like future joys to Fancy’s eye.”
Fig. 201.—View of Venice—Reflections.
397
That light moves in straight lines is a statement which is true only
when the media through which it passes are uniform; for it is easily
proved that when light passes from one medium to another, a change of
direction takes place at the common surface of the media in all rays that
meet this surface otherwise than perpendicularly. As a consequence of
this, it really is possible to see round a corner, as the reader may convince
himself by performing the following easy experiment. Having procured a
cup or basin, Fig. 202, let him, by means of a little bees’-wax or tallow,
attach to the bottom of the vessel, at R, a small coin. If he now places the
cup so that its edge just conceals the coin from view, and maintains his eye
steadily in the same position as at I, he
will, when water is poured into the cup,
perceive the coin apparently above the
edge of the vessel in the direction I R´,
that is, the bottom of the cup will appear
to have risen higher. Since it is
known that in each medium the rays
pass in straight lines, the bending which
renders the coin visible can therefore
only take place at the common junction
of the media, or, in other words, the
ray, R O, passing from the object in a
straight line through the water, is bent
abruptly aside as it passes out at the surface
of the water, A B, and enters the
air, in which it again pursues a straight
course, reaching the eye at I, where it
gives the spectator an impression of an object at R´. This experiment is also an
illustration of the cause of the well-known tendency we have to under-estimate
the depth of water when we can see the bottom. The broken appearance presented
by an oar plunged into clear water is due to precisely the same cause.
The curious exaggerated sizes and distorted shapes of the gold-fish seen in
a transparent globe have their origin in the same bending aside of the rays.
This deviation which light undergoes in passing obliquely from one medium
into another is known by the name of refraction, and it is essential for the
understanding of the sequel that the reader should be acquainted with some
of the laws of this phenomenon, although their discovery by Snell dates two
centuries and a half anterior to the present time. Let T O, Fig. 203, be a
ray of light which falls obliquely upon a plane surface, A B, common to two
different media, one of which is represented by the shaded portion of the
figure, A B C D, of which C D represents another plane surface, parallel to the
former. If the ray, T O, suffered no refraction, it would pursue its course
in a straight line to R´; but as a matter of fact it is found that such a ray is
always bent aside at O, if the medium A B C D is more or less dense than
the other. If, for example, A B C D is water, and the medium above it glass,
then the ray entering at O will take the course OR; but if A B C D is a plate
of glass with water above and below it, the ray will take the course T O,
O R, R B, suffering refraction on entering the glass, and again on leaving it,
398so that R B will emerge from the glass parallel to its original direction at T O.
If through the point of incidence, O, we suppose a line, O P, to be drawn
perpendicular to the surface, A B, then we may say that the ray in passing
from the rarer medium (water, air, &c.) into the denser medium (glass,
&c.) is bent towards the perpendicular, or normal, as at O; but that on
leaving the denser to enter the rarer medium, as at R, it is bent away from
the perpendicular. In other words, the angle bOa is less than the angle
mO T, and O R forms a less angle with R P´ than R B´ does. It is also a law
of ordinary refraction that the normal, O P, at the point of incidence, the
incident ray, T O, and the refracted ray, O R, are all in the same plane.
Besides, there is the important and interesting law discovered by Snell and
by Descartes, which may thus be explained with reference to Fig. 203. On
the incident and refracted rays, T O and O R, let us suppose that any equal
distances, Od and Ob, are measured off from O, and that from each of the
points a and b, perpendiculars, a m and b n, are drawn to the normal, P P,
which passes through O; then it is found that, whatever may be the angle
of incidence, T O P, or however it is made to vary, the length of the line
a m bears always the same proportion to the line b n for the same two media.
Thus, if A B C D be water, and T O enters it out of the air, the length of the
line a m divided by the length of the line a b will always (whatever slope
T O may have) give the quotient 1·33. This number is, therefore, a constant
quantity for air and water, and is called the index of refraction for air into
water. The law just explained is expressed by the language of mathematics
thus: For two given media the ratio of the sines of the angles of incidence
and of refraction is constant.
Fig. 202.
Fig. 203.
It is an axiom in optical science that a ray of light when sent in the opposite
direction will pursue the same path. Thus in Fig. 203 the direction
of the light is represented as from T towards B´; but if we suppose B´ R to be
an incident ray, it would pursue the path B´ R, R O, O T, and in passing out
of the denser medium, A B C D at O, its direction is farther from the normal,
P P, or O T, as the law of sines, a m will be always longer than n b, and will bear
a constant ratio to it. Suppose the angle R O P to increase, then P O B will
399become a right angle; that is, the emergent ray, O T, will just graze the surface,
A B, when the angle R O P has some definite value. If this last angle
be further increased, no light at all will pass out of the mediumA B C D, but
the ray R O will be totally reflected at O back into the medium, A B C D,
according to the laws of reflection. The angle which R O forms with O P
when O T just skims the surface, A B, is termed the limiting angle, or the
critical angle, and its value varies with the media. The reader may easily
see the total reflection in an aquarium, or even in a tumbler of water, when
he looks up through the glass at the surface of the water, which has then
all the properties of a perfect mirror.
The power of lenses to form images of objects is entirely due to these laws
of refraction. The ordinary double-convex lens, for example, having its
surfaces formed of portions of spheres, refracts the rays so that all the rays
which from one luminous point fall upon the lens, meet together again at a
point on the other side, the said point being termed their focus. It is thus
that images of luminous bodies are formed by lenses. An explanation of
the construction and theory of lenses cannot, however, be entered into in
this place.
One important remark remains to be made—namely, that in the above
statement of the laws of reflection and refraction, certain limitations and
conditions under which they are true and perfectly general have not been
expressed; for the mention of a number of particulars, which the reader
would probably not be in a condition to understand, would only tend to
confuse, and the explanation of them would lead us beyond our limits.
Some of these conditions belong to the phenomena we have to describe,
and are named in connection with them, and others, which are not in immediate
relation to our subject, we leave the reader to find for himself in
any good treatise on optics.
About two hundred years ago, a traveller, returning from Iceland,
brought to Copenhagen some crystals, which he had obtained from
the Bay of Roërford, in that island. These crystals, which are remarkable
for their size and transparency, were sent by the traveller to his friend,
Erasmus Bartholinus, a medical man of great learning, who examined them
with great interest, and was much surprised by finding that all objects
viewed through them appeared double. He published an account of this
singular circumstance in 1669, and by the discovery of this property of
Iceland spar, it became evident that the theory of refraction, the laws of
which had been studied by Snell and by Huyghens a few years before, required
some modification, for these laws required only one refracted ray, and
Iceland spar gave two. Huyghens studied the subject afresh, and was able,
by a geometrical conception, to bring the new phenomena within the general
theory of light. Iceland spar is chemically carbonate of lime (calcium carbonate),
and hence is also called calc spar, and, from the shape of the
crystals, it has also been termed rhombohedral spar. The form in which
the crystals actually present themselves is seen in Fig. 204, which also represents
the phenomenon of double refraction. Iceland spar splits up very
400readily, but only along certain definite directions, and from such a piece as
that represented in Fig. 204 a perfect rhombohedron, such as that shown in
Fig. 206, is readily obtained by cleavage; and then we have a solid having
six lozenge-shaped sides, each lozenge or side having two obtuse angles of
101° 55´, and two acute angles of 78° 5´. Of the eight solid corners, such
as A B C, &c., six are produced by the meeting of one obtuse and two acute
angles, and the remaining two solid corners are formed by the meeting of
three obtuse angles. Let us imagine that a line is drawn from one of these
angles to the other: the diagonal so drawn forms the optic axis of the
crystal, and a plane passing through the optic axis, A B, Fig. 205, and
through the bisectors of the angles, E A D and F B G, marks a certain definite
direction in the crystal, to which also belong all planes parallel to that
just indicated. Any one of such planes forms what is termed a “principal
section,” to which we shall presently refer.
Fig. 204.
Fig. 205.
Fig. 206.
It will be observed that in Fig. 204 the white circle on a black ground
seen through the crystal is doubled; but that, instead of being white as the
circle really is, the images appear grey, except where they overlap, and
there the full whiteness is seen. If we place the crystal upon a dot made
on a sheet of paper, or having made a small hole with a pin in a piece of
cardboard, hold this up to the light, and place the crystal against it, we see
apparently two dots or two holes. The two images will, if the dot or hole
be sufficiently small, appear entirely detached from each other. Now, if,
keeping the face of the crystal against the cardboard or paper, the observer
turn the crystal round, he will see one of the images revolve in a circle
round the other, which remains stationary. The latter is called the ordinary
image, and the former the extraordinary image. Let us place the crystal
upon a straight black line ruled on a horizontal sheet of paper, Fig. 205, and
let us suppose, in order to better define the appearance, that we place it
401so that the optic axis, A B, is in a plane perpendicular to the paper, A being
one of the two corners where the three obtuse angles meet, and B the other,
and the face, A B C D, parallel to E G H B, which touches the paper. Then,
according to the laws of ordinary refraction, if we look straight down upon
the crystal, we should see through it the line I K, unchanged in position—that
is, the ray would pass perpendicularly through the crystal as shown
by L M—and, in fact, a part of the ray does this, and gives us the ordinary
image, O O´; but another part of the ray departs from the laws of Snell
and Descartes, and, following the course L N Y´, enters the eye in the direction
N Y´, producing the impression of another line at L´, which is the extraordinary
ray, E E´. If the crystal be turned round on the paper, E E´
will gradually approach O O´, and the two images will coincide when the
principal section is parallel to the
line I K; but the coincidence is only
apparent, and results from the superposition
of the two images—for a
mark placed on the line drawn on the
paper will show two images, one of
which will follow the rotation of the
crystal, and show itself to the right
or left of the ordinary image, according
as C is to the right or left
of A. So that there are really in
every portion of the crystal two
images on the line, one of which
turns round the other, and the coalescence
of the two images twice in
each revolution is only apparent, for
the different parts of the lengths of
the images do not coincide. On continuing the revolution of the crystal after
they apparently coincide, the images are again seen to separate, the extraordinary
one being now displaced on the other side, or always towards the
point, C. Thus, then, the ray, on entering the crystal, bifurcates, one branch
passing through the crystal and out of it in the same straight line, just as it
would in passing through a piece of glass, while the other is refracted at
its entrance into the crystal, although falling perpendicularly upon its face,
and again at its exit. And again, when a beam of light, Rr, Fig. 206, falls
obliquely on a crystal of Iceland spar, it divides at the face of the crystal
into two rays, RO, and rE; the former, which is the ordinary ray, follows
the laws of ordinary refraction—it lies in the plane of incidence, and obeys
the law of sines, just as if it passed through a piece of plate-glass. The
extraordinary ray, on the other hand, departs from the plane of incidence,
except when the latter is parallel to the principal section, and the ratio of
the sines of the angles of incidence and refraction varies with the incidence.
The reader who is desirous of studying these curious phenomena of double
refraction, and those of polarization, is strongly recommended to procure
some fragments of Iceland spar, which he can very easily cleave into rhombohedra,
and with these, which need not exceed half an inch square, or cost
more than a few pence, he can demonstrate for himself the phenomena, and
become familiar with their laws. He will find very convenient the simple
plan recommended by the Rev. Baden Powell, of fixing one of the crystals
to the inside of the lid of a pill-box, through which a small hole has been
made, and through the hole and the crystal view a pin-hole in the bottom
402of the box, turning the lid, and the crystal with it, to observe the rotation
of the image. The same arrangement will serve, by merely attaching
another rhomb of spar within the box, to study the very interesting facts
of the polarization to which we are about to claim the reader’s attention.
The curious phenomena which have just been described, although in
themselves by no means recent discoveries, have led to some of the most
interesting and beautiful results in the whole range of physical science.
The examination and discussion of them by such able investigators as
Huyghens, Descartes, Newton, Fresnel, Malus, and Hamilton, have largely
conduced to the establishment of the undulatory hypothesis—that comprehensive
theory of light, which brings the whole subject within the reach of
a few simple mechanical conceptions.
It was at first supposed that it was only one of the rays which are produced
in double refraction that departed from the ordinary laws, and Iceland
spar was almost the only crystal known to have the property in question.
At the present day, however, the substances which are known to
produce double refraction are far more numerous than those which do not
possess this property, for, by a more refined mode of examination than the
production of double images, Arago has been able to infer the existence of
a similar effect on light in a vast number of bodies. Crystals have also
been found which split up a ray of light entering them into two rays, neither
of which obeys the laws of Descartes. It may, in fact, be said that, with
the exception of water, and most other liquids, of gelatine and other colloidal
substances, and of well-annealed glass, there are few bodies which do
not exercise similar power on light.
Fig. 207.
On examining the two rays which emerge from a rhomb of Iceland spar,
on which only one ray of ordinary light has been allowed to fall, we find
that these emergent rays have acquired new and striking properties, of
which the incident ray afforded no trace; for, if we allow the two rays
emerging from a rhomb of the spar to fall upon a second rhomb, we shall
find, on viewing the images produced, that their intensity varies with the
position into which its second crystal is turned. Thus, if we place a rhomb
of the spar upon a dot made on a sheet of white paper, we shall have, as
already pointed out, two images of equal darkness. But, in placing a second
rhomb of the spar upon the first, in such a manner that their principal
sections coincide, and the faces of one rhomb are also parallel to the faces
of the other, we shall still see two equally intense images of the dot, only
the images will be more widely separated than before, and no difference
will be produced by separating the crystals if the parallelism of the planes
of their respective principal sections be preserved. Here, then, is at once
a notable difference between a ray of ordinary light and one that emerges
from a rhomb of Iceland spar; for, in the case of rays of ordinary light, we
have seen that the second rhomb would divide each ray into two, whereas
it is incapable (in the position of crystals under consideration) of dividing
either the ordinary or the extraordinary ray which emerges from the first
rhomb. If, still keeping the second rhomb above the other, we make the
former rotate in a horizontal plane, we may observe that, as we turn the
upper crystal so that the planes of the principal sections form a small angle
with each, each image will be doubled, and, as the upper crystal is turned,
each pair of images exhibits a varying difference of intensity. The ordinary
ray in entering the second crystal is divided by it into a second ordinary
ray and a second extraordinary ray, the intensities of which vary according
to the angle between the principal sections. When the two principal
403sections are parallel to one plane, that is, when the angle between them is
either 0° or 180°, the extraordinary image disappears, and only the ordinary
one is seen, and with its greatest intensity. When the two principal sections
are perpendicular to each other, that is, when the second crystal has been
turned through either 90° or 270°, the extraordinary has, on the contrary,
its greatest intensity, and the ordinary one disappears. When the principal
section of the second crystal has been turned into any intermediate position,
such as through 45° and 135°, or any odd multiple of 45°, both images
are visible and have equal intensities. This experiment shows that the
two rays which emerge from the first crystal have acquired new properties,
that each is affected differently by the second crystal, according as the
crystal is presented to it in different directions round the ray as an axis.
The ray of light is no longer uniform in its properties all round, but appears
to have acquired different sides, as it were, in passing through the rhomb of
Iceland spar. This condition is indicated by saying that the ray is polarized,
and the first rhomb of spar is termed the polarizer, while the second rhomb,
by which we recognize the fact that both the ordinary and the extraordinary
rays emerge having different sides, has received the name of analyser. But,
in order to study conveniently all the phenomena in Iceland spar, we should
have crystals of a considerable size, otherwise the two rays do not become
sufficiently separated so as to make it an easy matter to intercept one of
them while we examine the other. A very ingenious mode of getting rid
of one of the rays was devised by Nicol, and as his apparatus is much used
for experiments on polarized light, we shall state the mode of constructing
Nicol’s Prism. It is made from a rhomb of Iceland spar, Fig. 207, in which
a and b are the corners where the three obtuse angles meet, all equal. If we
draw through a and b lines bisecting the angles d a c and f h g, and join a b,
these lines will all be in one plane, which is a principal section of the crystal,
and contains the axis, a b. Now suppose another plane, passing through a b,
to be turned so that it is at right angles to the plane containing a b and the
bisectors: this plane would cut the sides of the crystal in the lines a i, i h,
b k, k a; and in making the Nicol prism, the crystal is cut into two along
404this plane, and the two pieces are then cemented together by Canada balsam.
A ray of light, R, entering the prism, undergoes double refraction; but the
ordinary ray, meeting the surface of the Canada balsam at a certain angle
greater than the limiting angle, is totally reflected, and passes out of the
crystal at O; while the extraordinary ray, meeting the layer of balsam at a
less angle than its limiting angle, does not undergo total reflection, but
passes through the balsam, and emerges in the direction of E, completely
polarized, so that the ray is unable to penetrate another Nicol’s prism of
which the principal section is placed at right angles to that of the first.
Fig. 208.
Among other crystals which possess the property of doubly refracting, and
therefore of polarizing, is the mineral called tourmaline, which is a semi-transparent
substance, different specimens having different tints. In Fig. 208, A, B,
represent the prismatic crystals of tourmaline, and C shows a crystal which has
been cut, by means of a lapidary’s wheel, into four pieces, the planes of division
being parallel to the axis of the prism. The two inner portions form slices,
having a uniform thickness of about 1 20 in., and when the faces of these have
been polished, the plates form a convenient polarizer and analyser. Let
us imagine one of the plates placed perpendicularly between the eye and a
lighted candle. The light will be seen distinctly through it, partaking, however,
of the colour of the tourmaline; and if the plate be turned round so
that the direction of the axis of the crystal takes all possible positions with
regard to the horizon, while the plane of the plate is always perpendicular
to the line between the eye and the candle, no change whatever will be seen
in the appearance of the flame. But if we fix the plate of crystal in a given
position, let us say with the axial direction vertical, and place between it
and the eye the second plate of tourmaline, the appearances become very
curious indeed, and the candle is visible or invisible according to the position
of this second plate. When the axis of the second is, like that of the
first, vertical, the candle is distinctly seen; but when the axis of the second
plate is horizontal, no rays from the candle can reach the eye. If the second
plate be slowly turned in its own plane, the candle becomes visible or invisible
at each quarter of a revolution, the image passing through all degrees
of brightness. Thus the luminous rays which pass through the first plate
are polarized like those which emerge from a crystal of Iceland spar. It is
not necessary that the plates used should be cut from the same crystal of
tourmaline, for any two plates will answer equally well which have been
cut parallel to the axes of the crystals which furnished them. In the case
of tourmaline the extraordinary ray possesses the power of penetrating the
405substance of the crystal much more freely than the ordinary ray, which a
small thickness suffices to absorb altogether. It may be noted that in the
simple experiment we have just described, the plate of tourmaline next the
candle forms the polarizer, and that next the eye the analyser; and that
until the latter was employed, the eye was quite incapable of detecting the
change which the light had undergone in passing through the first plate, for
the unassisted eye had no means of recognizing that the rays emerged with
sides. The usual manner of examining light, to find whether it is polarized,
is to look through a plate of tourmaline or a Nicol’s prism, and observe
whether any change in brightness takes place as the prism or plate is
rotated. Now, it so happened that in 1808 a very eminent French man of
science, named Malus, was looking through a crystal of Iceland spar, and
seeing in the glass panes of the windows of the Luxembourg Palace, which
was opposite his house, the image of the setting sun, he turned the crystal
towards the windows, and instead of the two bright images he expected to
see, he perceived only one; and on turning the crystal a quarter of a revolution,
this one vanished as the other image appeared. It was, indeed, by
a careful analysis of this phenomenon that Malus founded a new branch of
science, namely, that which treats of polarized light; and his views soon
led to other discoveries, which, with their theoretical investigations, constitute
one of the most interesting departments of optical science, as remarkable
for the grasp it gives of the theory of light as for the number of
practical applications to which it has led.
The accidental observation of Malus led to the discovery that when a
ray of ordinary light falls obliquely on a mirror—not of metal, but of any
other polished surface, such as glass, wood, ivory, marble, or leather—it
acquires by reflection at the surface the same properties that it would acquire
by passing through a Nicol’s prism or a plate of tourmaline: in a
word, it is polarized. Thus, if a ray of light is allowed to fall upon a mirror
of black glass at an angle of incidence of 54° 35´, the reflected ray will be
found to be polarized in the plane of reflection—that is, it will pass freely
through a Nicol’s prism when the principal section is parallel to the plane
of reflection; but when it is at right angles to the latter, the reflected ray
will be completely extinguished by the prism—that is, it is completely
polarized. If the angle of the incident ray is different from 54° 35´, then
the reflected ray is not completely intercepted by the prism—it is not completely
but only partially polarized. The angle at which maximum polarization
takes place varies with the reflecting substance; thus, for water
it is 53°, for diamond 68°, for air 45°. A simple law was discovered by Sir
David Brewster by which the polarizing angle of every substance is connected
with its refractive index, so that when one is known, the other may
be deduced. It may be expressed by saying that the polarizing angle is
that angle of incidence which makes the reflected and the refracted rays
perpendicular to each other. The refracted rays are also found to be polarized
in a plane perpendicular to that of reflection.
Fig. 209.—Polariscope.
Fig. 210.
Fig. 211.—Iceland Spar showing Double Refraction.
Instruments of various forms have been devised for examining the phenomena
of polarized light. They all consist essentially of a polarizer and
an analyser, which may be two mirrors of black glass placed at the polarizing
angle, or two bundles of thin glass plates, or two Nicol’s prisms, or
two plates of tourmaline, or any pair formed by two of these. Fig. 209
represents a polariscope, this instrument being designed to permit any
desired combination of polarizer and analyser, and having graduations for
measuring the angles, and a stage upon which may be placed various substances
406in order to observe the effects of polarized light when transmitted
through them. It is found that thin slices of crystals placed between the polarizer
and analyser exhibit varied and beautiful effects of colour, and by such
effects the doubly refracting power of substances can be recognized, where
the observation of the production of double images would, on account of
their small separation, be impossible. And the polariscope is of great service
407in revealing structures in bodies which with ordinary light appear entirely
devoid of it—such, for example, as quill, horn, whalebone, &c. Except
liquids, well-annealed glass, and gelatinous substances, there are, in fact,
few bodies in which polarized light does not show us the existence of some
kind of structure. A very interesting experiment can be made by placing
in the apparatus, shown in Fig. 210, a square bar of well-annealed glass;
on examining it by polarized light, it will be found that before any pressure
from the screw C is applied to the glass, it allows the light to pass
equally through every part of it; but when by turning the screw the
particles have been thrown into a state of strain, as shown in the figure,
distinct bands will make their appearance, arranged somewhat in the
manner represented; but the shapes of the figures thus produced vary
with every change in the strain and in the mode of applying the pressure.
408
Fig. 212.
We have hitherto limited ourselves to a description of some of the
phenomena of light, without entering into any explanation of their
presumed causes, or without making any statements concerning the nature
of the agent which produces the phenomena. Whatever this cause or agent
may be, we know already that light requires time for its propagation, and
two principal theories have been proposed to explain and connect the facts.
The first supposes light to consist of very subtile matter shot off from
luminous bodies with the observed velocity of light; and the second theory,
which has received its great development during the present century,
regards luminous effects as being due to movements of the particles of
a subtile fluid to which the name of “ether” has been given. Of the
existence of this ether there is no proof: it is imagined; and properties
are assigned to it for no other reason than that if it did exist and possess
these properties, most of the phenomena of light could be easily explained.
This theory requires us to suppose that a subtile imponderable fluid pervades
all space, and even interpenetrates bodies—gaseous, liquid, and
solid; that this fluid is enormously elastic, for that it resists compression
with a force almost beyond calculation. The particles of luminous bodies,
themselves in rapid vibratory motion, are supposed to communicate movement
to the particles of the ether, which are displaced from a position
409of equilibrium, to which they return, executing backwards and forwards
movements, like the stalks of corn in a field over which a gust of wind
passes. While an ethereal particle is performing a complete oscillation, a
series of others, to which it has communicated its motion, are also performing
oscillations in various phases—the adjacent particle being a little behind
the first, the next a little behind the second, and so on, until, in the
file of particles, we come to one which is in the same phase of its oscillation
as the first one. The distance of this from the first is called the “length
of the luminous wave.” But the ether particles do not, like the ears of
corn, sway backwards and forwards merely in the direction in which the
wave itself advances: they perform their movements in a direction perpendicular
to that in which the wave moves. This kind of movement may
be exemplified by the undulation into which a long cord laid on the ground
may be thrown when one end is violently jerked up and down, when a wave
will be seen to travel along the cord, but each part of the latter only moves
perpendicularly to the length. The same kind of undulation is produced
on the surface of water when a stone is thrown into a quiet pool. In each
of these cases the parts of the rope or of the water do not travel along with
the wave, but each particle oscillates up and down. Now, it may sometimes
be observed, when the waves are spreading out on the surface of a
pool from the point where a stone has been dropped in, that another set of
waves of equal height originating at another point may so meet the first
set, that the crests of one set correspond with the hollows of the other, and
thus strips of nearly smooth water are produced by the superposition of the
two sets of waves. Let Fig. 212 represent two systems of such waves propagated
from the two points A A, the lines representing the crests of the
waves. Along the lines, b b, the crests of one set of waves are just over the
hollows of the other set; so that along these lines the surface would be
smooth, while along C C the crests would have double the height. Now, if
light be due to undulation, it should be possible to obtain a similar effect—that
is, to make two sets of luminous undulations destroy each other’s effects
and produce darkness: in other words, we should be able, by adding light
to light, to produce darkness! Now, this is precisely what is done in a
celebrated experiment devised by Fresnel, which not only proves that darkness
may be produced by the meeting of rays of light, but actually enables
us to measure the lengths of the undulations which produce the rays.
Fig. 213.
In Fig. 213 is a diagram representing the experiment of the two mirrors,
devised by Fresnel. We are supposed to be looking down upon the
arrangement: the two plane mirrors, which are placed vertically, being
seen edgeways, in the lines, M O, O N, and it will be observed that the
mirrors are placed nearly in the same upright plane, or, in other words, they
form an angle with each other, which is nearly 180°. At L is a very narrow
upright slit, formed by metallic straight-edges, placed very close together,
and allowing a direct beam of sunlight to pass into the apartment, this
being the only light which is permitted to enter. From what has been
already said on reflection from plane mirrors, it will readily be understood
that these mirrors will reflect the beams from the slit in such a manner as
to produce the same effect, in every way, as if there were a real slit placed
behind each mirror in the symmetrical positions, A and B. Each virtual
image of the slit may, therefore, be regarded as a real source of light at A
and at B; thus, for example, it will be observed that the actual lengths of
the paths traversed by the beams which enter at L, and are reflected from
the mirrors, are precisely the same as if they came from A and B respectively.
410The virtual images may be made to approach as near to each other as may
be required, by increasing the angle between the two mirrors, for, when
this becomes 180°, that is, when the two mirrors are in one plane, the two
images will coincide. If, now, a screen be placed as at F G, a very remarkable
effect will be seen; for, instead of simply the images of the two slits,
there will be visible a number of vertical coloured bands, like portions of
very narrow rainbows, and these coloured bands are due to the two sources
of light, A and B; for, if we cover or remove one of the mirrors, the bands
will disappear and the simple image of the slit will be seen. If, however,
we place in front of L a piece of coloured glass, say red, we shall no longer
see rainbow-like bands on the screen, but in their place we shall find a
number of strips of red light and dark spaces alternately, and, as before,
these are found to depend upon the two luminous sources, A and B. We
must, therefore, come to the conclusion that the two rays exercise a mutual
effect, and that, by their superposition, they produce darkness at some
points and light at others. These alternate dark and light bands are formed
on the screen at all distances, and the spaces between them are greater as
the two images, A and B, are nearer together. Further, with the same disposition
of the apparatus, it is found that when yellow light is used instead
of red, the bands are closer together; when green glass is substituted for
yellow, blue for green, and violet for blue, that the bands become closer
and closer with each colour successively. Hence, the effect of coloured
bands, which is produced when pure sunlight is allowed to enter at L, is
due to the superposition of the various coloured rays from the white light.
Let us return to the case of the red glass, and suppose that the distance
apart of the two images, A and B, has been measured, by observing the
angle which they subtend at C, and by measuring the distance, C O D, or
rather, the distance C O L. Now, the distances of A and B from the centre
of each dark band, and of each light band, can easily be calculated, and it
is found that the difference between the two distances is always the same for
the same band, however the screen or the mirrors may be changed. On
comparing the differences of the distances of A and B in case of bright bands,
with those in the case of dark ones, it was found that the former could be
expressed by the even multiples of a very small distance, which we will call
d, thus:
0, 2d, 4d, 6d, 8d, ...
411while the differences for the dark bands followed the odd multiples of the
same quantity, d, thus:
d, 3d, 5d, 7d, 9d, ....
These results are perfectly explained on the supposition that light is a kind
of wave motion, and that the distance, d, corresponds to half the length of
a wave. We have the waves entering L, and pursuing different lengths of
path to reach the screen at F G, and, if they arrive in opposite phases of
undulation, the superposition of two will produce darkness. The undulations
will plainly be in opposite phases when the lengths of paths differ by
an odd number of half-wave lengths, but in the same phase when they
differ by an even number. Hence, the length of the wave may be deduced
from the measurement of the distances of A and B from each dark and light
band, and it is found to differ with the colour of the light. It is also plain
that, as we know the velocity of light, and also the length of the waves, we
have only to divide the length that light passes over in one second, by the
lengths of the waves, in order to find how many undulations must take place
in one second. The following table gives the wave-lengths, and the number
of undulations for each colour:
Colour.
Number of Waves in one inch.
Number of Oscillations in one second.
Red
40,960
514,000,000,000,000
Orange
43,560
557,000,000,000,000
Yellow
46,090
578,000,000,000,000
Green
49,600
621,000,000,000,000
Blue
53,470
670,000,000,000,000
Indigo
56,560
709,000,000,000,000
Violet
60,040
750,000,000,000,000
These are the results, then, of such experiments as that of Fresnel’s, and
although such numbers as those given in the table above are apt to be considered
as representing rather the exercise of scientific imagination than
as real magnitudes actually measured, yet the reader need only go carefully
over the account of the experiment, and over that of the measurement
of the velocity of light, to become convinced that by these experiments
something concerned in the phenomena of light has really been measured,
and has the dimensions assigned to it, even if it be not actually the distance
from crest to crest of ether waves—even, indeed, if the ether and its waves
have no existence. But by picturing to ourselves light as produced by the
swaying backwards and forwards of particles of ether, we are better able
to think upon the subject, and we can represent to ourselves the whole of
the phenomena by a few simple and comparatively familiar conceptions.
As an example of the facility with which the ether theory lends itself
to aiding our notions of the phenomena of light, take the explanation of
polarization. Let us suppose that we are looking at a ray of light along
its direction, and that we can see the particles of ether. We should, in
such a case, see them vibrating in planes having every direction, and their
paths, as so seen, would be represented by an indefinite number of the
diameters of a circle. Now, suppose we make the ray first pass through a
412rhomb of Iceland spar: we should, if we could see the vibrating particles
in the emergent ordinary and extraordinary rays, perceive them swaying
backwards and forwards across the direction of the rays in two planes only,
as represented by the lines, B D and A C, in the two circles, Oo and Ee,
Fig. 214–-that is, half the particles would be vibrating in the direction B D,
and the other half in the direction A C; and further, the two directions
would be at right angles to each other—the vibrations forming the extraordinary
ray being performed in a plane at right angles to that in which the
vibrations producing the ordinary ray take place. If—these planes being
in the position indicated in 1, Fig. 214–-we turn the crystal round through
90°, they would rotate with it, and would come severally into the position
shown in 2, Fig. 214.
Fig. 214.
It was at one time objected to the theory which represents light as due
to wave-like movements that, just as the vibrations which constitute sound
spread in all directions, and go round intercepting bodies, enabling us, for
example, to hear the sound of a bell even when a building intervenes, so if
vibrations really produce light, these would extend within the shadows,
and we ought to perceive light within the shadows, bending, as it were,
round the edge of the shadow-casting body. This objection, which at one
time presented a great difficulty for the wave theory, was triumphantly removed
by the discovery that the luminous vibrations do extend into the
shadow, and that this is in reality never completely dark. It is true that,
although we can hear round a corner, we are in general unable to see round
it; but it should be noticed that in the case of hearing, the sound is much
weakened by intervening objects, and that there are what may be termed
sound shadows. A ray of light produces sensible effects only in the direction
of its propagation; but it can be shown that the successive portions
of the waves advancing along it are centres of lateral disturbances producing
new or secondary waves in all directions, which, however, interfere
with and destroy each other. When an opaque screen intercepts a portion
of the principal wave, it also stops a number of oblique or secondary waves,
which would interfere more or less with the rest. Under ordinary circumstances,
the remaining oblique or secondary rays are quite insensible in the
presence of the direct light. But, with an apparatus which will cost but
the two or three minutes’ time required to construct it, the reader may see
for himself that light is able to pass round an obstacle, and he may witness
directly phenomena of the same order as those presented in the experiment
of Fresnel’s mirrors, which require costly apparatus for their production.
He has only to take two fragments of common window-glass, and having
413made a piece of tinfoil adhere to one surface of each piece of glass, cut,
with a sharp penknife, the finest possible slit in each piece of tinfoil, making
the slit from ½ in. to 1 in. in length. If he will then hold one piece of glass
about 2 ft. from his eye, so that it may be in the line between his eye and the
sun (or other luminous body), and hold the other piece close to his eye with
its slit parallel to that in the first piece, he will see the latter not simply as
a line of light, but parallel to it a number of brilliantly-coloured rainbow-like
bands will be seen on either side. If, instead of receiving the light
from the sun, or from a candle-flame, the light given off by a spirit-lamp,
with a piece of salt on its wick, be used, bright yellow stripes will be seen
with dark spaces between them. Or, if the piece of glass next the sun be
red-coloured, instead of plain glass, no rainbow-like bands will be visible,
but a number of bright red stripes alternating with dark bands will be seen.
The reader will have probably now little difficulty in perceiving that these
can be easily explained as the results of interferences of a kind quite analogous
to those of the waves of water represented in the diagram, Fig. 212.
The rainbow-like stripes are due to the different wave-lengths of the different
colours, as a consequence of which the bright and dark bands would
be formed at different positions. Our limits do not admit of a full explanation
of these beautiful effects, but the reader requiring further information
would peruse with the greatest advantage portions of Sir John Herschel’s
“Familiar Lectures on Scientific Subjects.”
The undulatory theory gives also an easy explanation of colours; they
being, according to the theory, only the effects, as already stated, of the
different rates of vibrations of the ether. If the ether particles perform
514,000,000,000,000 oscillations in a second, we receive the impression we
call red colour; if they execute 750,000,000,000,000 vibrations, the impression
produced on our organ of sight is different—we call it violet; and so on.
Thus science teaches us that visual impressions so different as red, green,
blue, violet, and other distinct colours, are, in reality, all due to movements
of one and the same——something; and that the different sensations
of colour we experience, arise merely from different rates of recurrence in
these movements. In the subsequent article we shall have occasion to
show that ordinary light, such as that of the sun, or of a candle, contains
rays of every imaginable colour, mixed together in such proportions, that
when this light falls upon a piece of paper, or upon snow, we have, in looking
at these objects, the sensation of whiteness. But, if the light falls upon
any substance which is able, in some way, to absorb or destroy some of the
vibrations, the admixture of which makes up “white light,” as it is called,
then that object sending back to our eyes the rays formed of the remaining
group of vibrations, gives us the sensation of colour. Suppose, for
example, a substance to be so constituted that it is capable of absorbing, or
quenching in some way, all the vibrations of the ether which occur at a
quicker rate than 520,000,000,000,000 in a second: such a substance would
send back to our eyes only the vibrations which constitute red light (see
table, page 411), and we should say the substance in question had a red
colour. Similarly, if the substance gave back only the vibrations which
have the quickest rates, we should call the substance of a violet character.
The agent which produces in our visual organs the impression of colour is,
therefore, not in the objects, but in the light which falls upon them. The
rose is red, not because it has redness in itself, but because the light which
falls upon it contains some rays in which there are movements that occur
just the number of times per second that gives us the impression we call
414redness; in short, the colour comes not from the flower but from the light.
“But,” the reader might say, “the rose is always red by whatever light I
see it, and therefore the colour must be in the flower. Whether I view it
by sunlight, or moonlight, or candlelight, or gaslight, I invariably see that
it is red.” Now, it is precisely this circumstance—the seemingly invariable
association of the object with a certain impression—in this case, redness—that
leads our judgment astray, and makes us believe that the colour
is in the object. Most people live out their lives without anything occurring
to them which would give them the least idea that the colours of the
objects they see around them are not in these objects themselves, but are
derived from the light that falls upon the objects. And it required the
comparison of many observations and experiments, and some clear reasoning,
to establish a truth so unlike the most settled convictions of ordinary
minds.
The point in question is fortunately one extremely easy of experiment,
since we have simple means of producing light in which the vibrations corresponding
to only one colour are present. The reader is strongly recommended
to try the following experiment for himself. Let him procure a
spirit-lamp, and place on the wick a piece of common salt about as large
as a pea. Let the lamp be lighted in a room from which all other light is
completely excluded, and bring near the flame a red rose or a scarlet geranium.
The flower will be seen with all its redness gone—it will appear
of an ashy grey or leaden colour. A ball of bright scarlet wool, such as
ladies use to work brilliant patterns for cushions, &c., held near this flame,
is apparently transformed into a ball of the homely grey worsted with which,
about a century ago, old ladies might be seen industriously darning stockings.
The experiment is, perhaps, even more striking when, a little distance
from the spirit-lamp, is placed a feeble light of the ordinary kind, a
rushlight for example. The ball of wool, held near the latter, shows vivid
scarlet, but, brought near the spirit-lamp with the salted wick, is pale, ashy
grey. Moving thus the ball of worsted, first to one light then to the other,
gives a most convincing and striking proof of the entire illusion we are
under as to colour being an inherent quality of substances. Similar experiments
may be multiplied indefinitely. A bouquet, viewed by the rushlight,
shows the so-called natural colours of the flowers; viewed by the salted
flame, roses, verbenas, violets, larkspurs, and leaves, all appear of the
uniform ashy grey, and only yellow flowers come out in their natural
colours. A picture, say a chromo-lithograph after one of the most gorgeous
landscapes that Turner ever painted, appears a work in monochrome, and
gives exactly the effect of a sepia or indian-ink drawing. The most blooming
complexion vanishes, and the countenance assumes a cadaverous aspect
very startling to persons of weak nerves; the lips especially, which might
have rivalled pink coral by ordinary light, take a repulsive livid hue. All
these effects may be seen to greater advantage by using the gas-flame of a
Bunsen’s burner, having a lump of salt placed in the flame; or by means of
a piece of fine wire gauze, about six inches square, supported about two or
three inches above an ordinary gas-burner, from which the gas is allowed
to issue without being lighted, but when to the top of the wire gauze, which
is strewed with small fragments of salt, a light is applied, the gas will ignite
only above the gauze, without the flame passing down to the burner below.
A fuller explanation of these strange appearances may be gathered from
the subsequent article; but it may suffice now to state that spirit, or gas
burned in the way we have indicated, gives off little or no light of any kind.
415If, however, common salt be introduced into the flame, then light—but
light of only one particular colour—is given off, and that colour is yellow.
There are no red, or green, or blue, or violet vibrations given off; and as
the objects on which the light falls cannot supply these, it follows that with
this light no impression corresponding to these colours can be produced
on the eye, whatever may be the objects upon which it falls. Such experiments,
not simply read about but actually performed, cannot fail to convince
an intelligent person that the colours come from the light and not from the
object. Of course, it is not denied that there is in each substance something
that determines which are the rays absorbed, and which are the rays
reflected to the eye—something that can destroy certain waves, but is
powerless over others that rebound from the substance, and reaching the
eye, there produce their characteristic impressions. And it is but this power
of sending back only certain rays among the multitude which a sunbeam
furnishes, that can be attributed to objects when we say that they have
such or such a colour. In this sense, then, we may properly say that the
rose is red, but it is also at the same time undeniably true that the redness
is not in the rose.
Let it not be supposed that such scientific conclusions as those we have
arrived at tend in any way to rob Nature of her beauty, or that our sense
of the loveliness of colour is in any danger of being blunted by thus tracing
out, as far as may be, the causes and sources of our sensations. The poets
have occasionally said harsh things of science—indeed, one goes so far as
to stigmatize the man of science as one who would “untwist the rainbow”
and “botanize upon his mother’s grave;” and another thus laments dispelled
illusions:
“When Science from Creation’s face
Enchantment’s veil withdraws,
What lovely visions yield their place
To cold material laws!”
Now, in the case we have been considering, the scientific view is surely
as beautiful as the ordinary one. We can, it is true, no longer regard the
objects as having in themselves the colours which common observation
attributes to them, but we look upon the material world as being, so to
speak, the neutral canvas upon which Light, the great painter, spreads
his varied tints, although, unlike the real canvas of an artist, which is not
only neutral, but receives indifferently whatever hues are laid upon it, the
objects around us exercise a selective effect—as if the picture of Nature
were produced by each part of the canvas refusing all the tints save one,
but itself supplying none. The tendency of the study of science to increase
our interest in the great spectacle of Nature, and to enhance our appreciation
of her charms, has been more justly indicated by another poet—thus:
“Nor ever yet
The melting rainbow’s vernal tinctured hues
To me have shone so pleasing, as when first
The hand of Science pointed out the path
In which the sunbeams gleaming from the west
Fall on the watery cloud, whose darksome veil
Involves the orient.”
416
Fig. 215.—Portrait of Professor Kirchhoff.
THE SPECTROSCOPE. — CELESTIAL CHEMISTRY AND PHYSICS.
Many of the modern discoveries and inventions already described in
these pages have been instances of practical applications of science
to the every-day wants of mankind; but the chief interest of the subject
we now enter upon flows mainly from other sources than direct applications
of its principles in useful arts, although these applications are already neither
few nor unimportant. But that which, in the highest degree, claims our attention
and excites our admiration in the revelations of the spectroscope is the
wonderful and wholly unexpected extent to which this instrument has enlarged
our knowledge of the universe, and the apparently inadequate means
by which this has been accomplished. A little triangular piece of glass
gives us power to rob the stars of their secrets, and tells more about those
distant orbs than the wildest imagination could have deemed attainable to
human knowledge. One of the most acute philosophers of the present
century, a profound thinker who devoted his mind to the consideration of
the mutual relations of the sciences, declared emphatically, not very many
years ago, that all we could know of the heavenly bodies must ever be confined
to an acquaintance with their motions, and to such a limited acquaintance
with their features as the telescope reveals in the less distant ones.
417A knowledge of their composition, he expressly asserted, could never be
attained, for we could have no means of chemically examining the matter
of which they are constituted. Such was the deliberate utterance of a man
by no means disposed to underrate the power of the human mind in the
pursuit of truth. And such might still have been the opinion of the learned
and of the unlearned, but for the remarkable train of discoveries which has
led us to the construction of instruments revealing to us the nature of the
substances entering into the constitution of the heavenly bodies. We have
now, for example, the same certainty about the existence of iron in our
sun, that we have about its existence in the poker and tongs on the hearth.
The last few years have seen the dawn of a new science; and two branches
of knowledge which formerly seemed far as the poles asunder—namely,
astronomy and chemistry—have their interests united in this new science of
celestial chemistry. The progress which has been made in this department
of spectroscopic research is so rapid, and the field is so promising,
that the well-instructed juvenile of the future, instead of idly repeating the
simple lay of our childhood:
“Twinkle, twinkle, little star,
How I wonder what you are!”
will probably only have to direct his sidereal spectroscope to the object of
his admiration in order to obtain exact information as to what the star is,
chemically and physically.
Fig. 216.
The results which have already been obtained in celestial chemistry, and
other branches of spectroscopic science, are so surprising, and apparently
so remote from the range of ordinary experience, that the reader can only
appreciate these wonderful discoveries by tracing the steps by which they
have been reached. A few fundamental phenomena of light have already
been spoken of in the foregoing article; and an acquaintance with these
will have prepared the reader’s mind
for a consideration of the new facts
we are about to describe. In discussing,
in the foregoing pages, the subject
of refraction, we have, in order
that the reader’s attention might not
be distracted, omitted all mention of
a circumstance attending it, when a
beam of ordinary light falls upon a
refracting surface, such as that represented
in Fig. 203. The laws
there explained apply, in fact, to elementary
rays, and not to ordinary
white light, which is a mixture of a
vast multitude of elementary rays,
red, yellow, green, &c. When such
a beam falls obliquely upon a piece
of glass, the ray is, at its entrance,
broken up into its elements, for these,
being refracted in different degrees
by the glass, each pursues a different
path in that medium, as represented by Fig. 216. Each elementary ray
obeys the laws which have been explained, and therefore each emerges
from the second surface of the plate parallel to the incident ray, and, in
418consequence of this, the separation is not perceptible under ordinary circumstances
with plates of glass having parallel surfaces. But, if the second
surface be inclined so as to form such an angle with the first that the rays
are rendered still more divergent in their exit, then the separation of the
light into its elementary coloured rays becomes quite obvious. Such is
the arrangement of the surfaces in a prism, and in the triangular pieces of
glass which are used in lustres.
For the fundamental experimental fact of our subject, we must go back
two centuries, when we shall find Sir Isaac Newton making his celebrated
analysis of light by means of the glass prism. We shall describe Newton’s
experiment, for, although it was performed so long ago, and is generally
well known, it will render our view of the present subject more complete;
and it will also serve to impress on the reader an additional instance of
the world’s indebtedness to that great mind, when we thus trace the grand
results of modern discovery from their source. “It is well,” is the remark
of a clear thinker and eloquent writer, “to turn aside from the fretful din
of the present, and to dwell with gratitude and respect upon the services of
‘those mighty men of old, who have gone down to the grave with their
weapons of war,’ but who, while they lived, won splendid victories over
ignorance.”
Fig. 217.—Newton’s Experiment.
The experiment of Sir Isaac Newton will be readily understood from
Fig. 217, where C is the prism, and A C represents the path of a beam of
sunlight allowed to enter into a dark apartment through a small round
hole in a shutter, all other light being excluded from the apartment. In
this position of the prism, the rays into which the sunbeam is broken at
its entrance into the glass were bent upwards, and at their emergence from
the glass they were again bent upwards, still more separated, so that when
a white screen was placed in their path, instead of a white circular image
of the sun appearing, as would have been the case had the light been
merely refracted and not split up, Newton saw on the screen the variously-coloured
band, D D, which he termed the spectrum. The letters in the
figure indicate the relative positions of the various colours, red, orange,
yellow, green, blue, &c., by their initial letters. The spectrum, or prolonged
419coloured image of the sun, is red at the end, R, where the rays are
least refracted, and violet at the other extremity, where the refraction is
greatest, while, in the intermediate spaces, yellow, green, and blue pass by
insensible gradations into each other. Newton varied his experiment in
many ways, as, for example, by trying the effect of refraction through a
second prism on the differently coloured rays. He found that the second
prism did not divide the yellow rays, for instance, into any other colour,
but merely bent them out of the straight course, to form on the second
screen a somewhat broader band of yellow, and similarly with regard to the
others. From these, and a number of other experiments described in his
“Opticks,” (A. D. 1675), Newton concludes, “that if the sun’s light consisted
of but one sort of rays, there would be but one colour in the whole world,
nor would it be possible to produce any new colour by reflections and refractions,
and, by consequence, the variety of colours depends upon the
composition of light.” ... “And if, at any time, I speak of light and
rays, or coloured, or endued with colours, I would be understood to speak
not philosophically and properly, but grossly, and accordingly to such conceptions
as vulgar people in seeing all these experiments would be apt to
frame. For the rays, to speak properly, are not coloured. In them there
is nothing else than a certain power and disposition to stir up a sensation
of this or that colour. For, as sound in a bell, a musical string, or other
sounding body, is nothing but a trembling motion, and in the air nothing
but that motion propagated from the object, and in the sensorium ‘tis a
sense of that motion under the form of a sound; so colours in the object
are nothing but a disposition to reflect this or that sort of rays more copiously
than the rest: in the rays they are nothing but their dispositions to
propagate this or that motion into the sensorium, and in the sensorium
they are sensations of these motions under the form of colours.”
These memorable investigations of Newton’s have been the admiration
of succeeding philosophers, and even poets have caught inspiration from
this theme:
“Nor could the darting beam of speed immense
Escape his swift pursuit and measuring eye.
E’en Light itself, which everything displays.
Shone undiscovered, till his brighter mind
Untwisted all the shining robe of day;
And, from the whitening undistinguished blaze,
Collecting every ray into his kind,
To the charmed eye educed the gorgeous train
Of parent colours. First the flaming red
Sprung vivid forth; the tawny orange next;
And next delicious yellow—by whose side
Fell the kind beams of all-refreshing green;
Then the pure blue, that swells autumnal skies,
Ethereal played; and then, of sadder hue
Emerged the deepened indigo, as when
The heavy-skirted evening droops with frost,
While the last gleamings of refracted light
Died in the fainting violet away.
These, when the clouds distil the rosy show,
Shine out distinct adown the watery bow;
While o’er our heads the dewy vision bends
Delightful—melting on the fields beneath.
Myriads of mingling dyes from these result,
And myriads still remain.—Infinite source
Of beauty! ever blushing—ever new!
Did ever poet image aught so fair,
Dreaming in whispering groves, by the hoarse brook,
Or prophet, to whose rapture Heaven descends?”
The spectra which Newton obtained by admitting the solar beams
420through a circular aperture, were, however, not simple spectra. The circular
beam may be considered as built up of flat and very thin bands of
light, parallel to the edges of the prism, and a simple ray would be formed
by one of these flat bands; as the round opening would allow an indefinite
number of such rays to enter, each would produce its own spectrum on the
screen, and the actual image would be formed of a number of spectra
overlapping each other. When the aperture by which the light is admitted
consists merely of a narrow slit, or line, parallel to the edges of the prism,
we obtain what is termed a pure spectrum. When the prism is properly
placed, an eye, viewing the fine slit through it, sees a spectrum formed, as
it were, of a succession of virtual images of the slit in all the elementary
coloured rays.
The person who first examined the solar spectrum in this manner was the
English chemist Wollaston, who, in 1802, found that the spectrum thus observed
was not continuous, but that it was crossed at intervals by dark lines.
Wollaston saw them by placing his eye directly behind the prism. Twelve
years later, namely, in 1814, the German optician Fraunhofer devised a
much better mode of viewing the spectrum; for, instead of looking through
the prism with the naked eye, he used a telescope, placing the prism and
the telescope at a distance of 24 ft. from the slit, the virtual image of which
was thus considerably magnified. The prism was so placed that the incident
and refracted rays formed nearly equal angles with its faces, in
which circumstance the ray is least deflected from its direction, and the
position is therefore spoken of as being that of minimum deviation. It
can be shown that this position is the only one in which the refracted rays
can produce clear and sharp virtual images of the slit, and therefore it is
necessary in all instruments to have the prism so adjusted. Fraunhofer
then saw that the dark lines were very numerous, and he found that they
always kept the same relative positions with regard to the coloured spaces
they crossed; that these positions did not change when the material of
which the prism was made was changed; and that a variation in the refracting
angle of the prism did not affect them. He then made a very
careful map, laying down upon it the position of 354 of the lines out of about
600 which he counted, and indicated their relative intensities, for some
are finer and less dark than others. The most conspicuous lines he distinguished
by letters of the alphabet, and these are still so indicated; and
the dark lines in the solar spectrum are called “Fraunhofer’s Lines.” These
lines, as will appear in the sequel, are of great importance in our subject.
A few of the more obvious ones are shown in No. 1, Plate XVII. Fraunhofer
found that these lines were always produced by sunlight, whether
direct, or diffused, or reflected from the moon and planets; but that the
light from the fixed stars formed spectra having different lines from those
in the sun—although he recognized in some of the spectra a few of the
same lines he found in the solar spectrum. The fact of these differences
in the spectra of the sun and fixed stars proved that the cause of the dark
lines, whatever it might be, must exist in the light of these self-luminous
bodies, and not in our atmosphere. It was, however, some years afterwards
ascertained that the passage of the sun’s light through the atmosphere
does give rise to some dark bands in the spectrum; for it was found that
certain lines make their appearance only when the sun is near the horizon,
and its rays consequently pass through a much greater thickness of air.
Sir D. Brewster first noticed in 1832 that certain coloured gases have the
power of absorbing some of the sun’s rays, so that the spectrum, when the
421rays are made to pass through such a gas before falling on the prism, is
crossed by a series of dark lines—altogether different from Fraunhofer’s
lines, though these are also present. The gas in which this property was
first noticed is that called “nitric peroxide”—a brownish-red gas, of which
even a thin stratum produces a well-marked series of dark lines. The same
property was soon discovered in the vapours of bromine, iodine, and a certain
compound of chlorine and oxygen. Each substance furnishes a system
of lines peculiar to itself: thus the vapour of bromine, although it has almost
exactly the same colour as nitric peroxide, gives a totally different set of
lines. These, therefore, do not depend on the mere colour of the gas or
vapour, and this is conclusively proved by the fact of many coloured vapours
producing no dark lines whatever: the vapour of tungsten chloride, for
example, although in colour so exactly like bromine vapour that the two
cannot be distinguished by the eye, yields no lines whatever.
Fig. 218.—Bunsen’s Burner on a stand.
In Fig. 218 is represented a lamp for burning coal-gas, which is constantly
used by chemists as a source of heat. It is known as “Bunsen’s
burner,” from its inventor the celebrated German chemist. It consists of
a metal tube, 3 in. or 4 in. long, and ⅓ in.
in diameter, at the bottom of which the
gas is admitted by a small jet communicating
with the elastic tube which brings
the gas to the apparatus. A little below
the level of the jet there are two lateral
openings which admit air to the tube.
The gas, therefore, becomes mixed with
air within the tube, and this inflammable
mixture streams from the top of the tube
and readily ignites on the approach of a
flame, the mixture burning with a pale
bluish flame of a very high temperature.
This little apparatus is not only the most
useful pieces of chemical apparatus ever
devised, but it furnishes highly instructive
illustrations of several points in
chemical and physical science; and to
some of these we invite the reader’s
attention, as they have an immediate
bearing on our present subject. Coal-gas
is a mixture of various compounds of
the two elementary bodies, hydrogen and carbon; and when the gas burns,
these substances are respectively uniting with the oxygen of the air, producing
water and carbonic acid gas. Now, when coal-gas is burnt in the
ordinary manner as a source of light, the supply of oxygen is too small to
admit of the complete combustion of all its constituents; and as the oxygen
more eagerly seizes upon the hydrogen than upon the carbon, a large proportion
of the latter thus set free from its hydrogen compound is deposited
in the flame in the solid form, and is there intensely heated. The presence
of solid carbon in an ordinary gas flame is easily proved by holding in it a
cold fragment of porcelain, or a piece of metal, which will become covered
with soot. In the flame of the Bunsen burner there is no soot, because the
increased supply of oxygen, afforded by previously mixing the gas with air,
enables the whole of the constituents of the gas to be completely burnt;
and this is of the greatest advantage to the chemist, who always desires to
422have the vessels he heats free from soot, in order that he may observe what
is taking place within them. The flame of Bunsen’s lamp becomes that of
an ordinary sooty gas flame, when the two orifices which admit the air at
the bottom of the tube are closed up, and then, of course, the temperature
cannot be so high as when the whole constituents of the gas are completely
burnt, but the flame becomes highly luminous; whereas when the
orifices are open it gives so little light, that in a dark room one cannot see
a finger held 20 in. from the lamp. Plainly the cause of this difference is
connected with the presence or absence of the heated particles of solid
carbon. The non-luminous flame contains no solid particles; the bright
part of the other flame is full of them. To these heated particles of solid
carbon we are, then, indebted for the light which burning coal-gas supplies.
And, since we are able by such artificial illumination to distinguish colours,
the white-hot carbon must give off rays of all degrees of refrangibility, and
we should expect to find in the spectrum produced by such a flame, the red,
yellow, green, and other coloured rays. And such is indeed the spectrum
which these incandescent carbon particles produce: it resembles the solar
spectrum, but there is an entire absence of dark lines, so that the appearance
is that represented in No. 1, Plate XVII., if we suppose the Fraunhofer
lines removed. If the pale blue flame of the Bunsen’s burner be similarly
examined, the spectrum, No. 14, Plate XVII., shows that only a few rays of
certain refrangibilities are emitted, forming bright lines here and there, but
of little intensity, while the whole of the other rays are absent. This shows
that while the highly heated solid gives off all rays from red to violet without
interruption, the still more highly heated gases give off only a few
selected rays.
It has long been known that some substances impart certain colours
to flames, and such substances have been long employed to produce
coloured effects in fireworks, &c. But coloured flames do not appear to
have been examined by the prism until 1822, when Sir John Herschel
described the spectra of strontium, copper, and of some other substances,
remarking that “The colours thus communicated by the different bases to
flame afford in many cases a ready and neat way of detecting extremely
minute quantities of them.” A few years later, Fox Talbot described the
method of obtaining a monochromatic flame, by using in a spirit-lamp
diluted alcohol in which a little salt has been dissolved. The paper in which
he describes this and other observations concludes thus: “If this opinion
should be correct and applicable to the other definite rays, a glance at the
prismatic spectrum of flame may show it to contain substances which it
would otherwise require a laborious chemical analysis to detect.” Here we
have the first hint of that spectrum analysis which has provided the chemist
with a method of surpassing delicacy for the detection of metallic elements.
The spectra of coloured flames were also subsequently examined and
described by Professor W. A. Miller, but the most complete investigation
into the subject was made by Professors Kirchhoff and Bunsen, who also
contrived a convenient instrument, or spectroscope, for the examination and
comparison of different spectra. The instrument has received many improvements
and modifications, but the essential parts are one or more
prisms; a slit, through which the light to be examined is allowed to enter; a
tube, having at the other end a lens to render parallel the rays from the slit;
a telescope, through which the spectrum is viewed; and usually some apparatus
by which the positions of the different lines may be identified.
PLATE XVII. SPECTRA.
Fig. 219.—Spectroscope with one Prism.
A very elegant instrument, made by Mr. John Browning, of the Strand, is
423represented in Fig. 219. It has a single prism, made of glass, of great power
in dispersing the rays. The prism is supported on a little stage, placed in the
middle of a horizontal circular brass table about 6 in. in diameter. On the
left is seen a tube, about 15 in. long, at the outer extremity of which is the
slit, formed of pieces of metal very accurately shaped. One of these pieces
slides in a direction at right angles to the slit, and, by means of a spring
and a fine screw, can be very nicely adjusted, so that an opening of any
degree of fineness can be readily obtained. In front of the slit is a small
glass prism, with its edges parallel to the slit, but only half its height. The
bases of this prism are formed of two sides of a square and its diagonal,
and, as shown in the figure, one side is parallel to the face of the slit, and
the other to the axis of the tube. Rays of light coming from a source on
the left of the slit (as seen in the figure) will, therefore, enter this little
prism, and be totally reflected (see page 399) by the diagonal surface, down
the axis of the tube through the lower half only of the slit. This is the
only office of this prism, which has nothing to do with the dispersion of the
rays: the use to which it is put will be seen presently. It is fixed in such
a manner that, when required, it can be turned aside with the touch of a
finger, and the whole length of the slit exposed. A peculiarity in these
instruments of Mr. Browning’s is the admirable arrangement for determining
the position of any line in a spectrum. For this purpose, the eye-piece
of the telescope is provided with a pair of cross-wires, and the telescope
itself, which is about 18 in. in length, moves in a horizontal plane
round the axis of the circular brass table, from which an arm projects,
carrying a ring into which the telescope screws. This arm carries a vernier
along the limb of the circular table, which is very accurately divided into
thirds of degrees, so that with the aid of the vernier the angular position
of the telescope can be read off to a minute, that is, to 1 60th of a degree. The
arm carrying the telescope is provided with a screw for clamping it in any
desired position while the readings are taken. On placing in front of the
slit the flame of a Bunsen’s burner, the spectrum produced by any substance
in this flame will, when the instrument is in proper adjustment, be seen on
424looking through the telescope, and the cross-wires being also in view, the
point of their intersection may be brought into coincidence with any line of
the spectrum, and the telescope being clamped in this position, the angular
reading thus taken determines the position of the line. Thus, for example,
the angular positions in which the principal Fraunhofer’s lines are seen
having been observed and recorded, the angular position of any line in another
spectrum will at once determine its position among the Fraunhofer
lines; or the spectrum may be mapped by laying down the angular readings
of the lines by means of a scale of equal parts. And, again, in the
little prism in front of the slit we have the means of bringing two spectra
in view at once, one being from a light directly in front, and the other from
a light at the side. The two spectra are seen one above the other, and the
coincidence or difference of their lines may be directly observed. When the
instrument is in use, the prism and the ends of the tube are covered with
a black cloth, loosely thrown over them, by which all stray light is shut out.
The author has had in use for several years one of these instruments, and
he cannot forbear expressing his perfect satisfaction with its powers, which
he finds amply sufficient for all ordinary chemical purposes, while the accuracy
of the workmanship is really wonderful, considering the very moderate
price of the instrument.
The substances the spectra of which are most conveniently examined are
the metals of the alkalies and alkaline earths. Small quantities of the salts
of these metals, placed in a loop of fine platinum wire, impart characteristic
colours to the flame of a Bunsen burner or to that of a spirit-lamp. For the
examination of the spectra the former is to be preferred, as the lines come
out much more vividly. Indeed, at temperatures higher than that of the
Bunsen’s burner, such as in the flame of pure hydrogen, or in the voltaic
arc, some substances give out additional lines. In Plate XVII., Nos. 2 to 9,
is shown the appearance of the spectra produced by the Bunsen’s burner
when salts of the metals are held in the flame in the manner already mentioned,
and the spectra are examined with the instrument just described.
One of the simplest of these spectra is that produced by sodium compounds,
such as common salt. The smallest particle of this substance imparts an
intense yellow colour to the flame, and the spectrum is found to take the
form of a single bright yellow line—No. 3. It has been estimated that the
presence of the (1 100000000)th part of a grain of sodium can be detected by
the production of this line. Indeed, the very delicacy of this sodium reaction
renders it almost impossible to get rid of this line, for sodium is
found to be present in almost everything,—a fact the earlier observers of
spectra were not aware of, for they attributed this yellow line to water,
which was the only substance they knew to be so generally diffused. If a
platinum wire be heated in the flame of the Bunsen burner until all the
sodium indications have disappeared, it suffices to remove the wire, and,
without allowing it to come into contact with anything, to leave it exposed
to the air for a few minutes, to cause it again to give the characteristic
yellow colour when again plunged into the flame. This is due to the fact
that the element is contained in all the floating particles which pervade
the atmosphere. The spectroscope is not required to show the presence of
the sodium on the platinum which has been exposed to the air, the colour
imparted to the flame being plainly visible to the eye, and it needs only the
Bunsen burner and 2 in. of platinum wire to prove the fact, and also to show
that mere contact with the fingers is enough to highly charge the wire with
sodium compounds. Any volatile compound of potassium gives the spectrum
425represented by No. 2, the principal lines being a red line and one in
the extreme violet, the latter being somewhat difficult to observe. There
is also a third rather ill-defined red line, and a portion of a faint continuous
spectrum. Salts of strontium impart a bright red colour to the flame, and
the spectrum they produce is shown by No. 6, in which are seen several
bright red lines and a fainter blue one. Calcium, which also gives a reddish
colour to flame, furnishes an entirely different set of lines (No. 5), and
barium salt another, containing numerous lines, especially some very vivid
green ones.
In all the cases we have named, and whenever bright-lined spectra are
furnished by substances placed in the flame of a lamp, or in burning hydrogen
gas, or in the intensely hot voltaic arc, there is evidence that the substances
are converted into vapour or gas. We have already seen how hot
solid carbon gives a continuous spectrum, while carbon in the state of
gaseous combination gives most of the bright lines seen in the spectrum
of coal-gas (No. 14). It is observed also that the more readily volatized
are the salts, the more vivid are the bright lines they produce when heated
in a flame. It must be understood that each element gives it own characteristic
lines, that these are always in precisely the same position in the
spectrum, that no substance produces a line in exactly the same position as
another, however near two lines due to different substances may, in some
cases, appear; and also, that however the salts of the different metals are
mixed together, each produces its own lines, and each ingredient may be
recognized. And this is done in an instant by an experienced observer—a
mere glance at the superposed spectra of, perhaps, half a dozen metals,
suffices to inform him which are present. There is also a peculiarity in
this optical mode of recognizing the presence of bodies which gives the
subject the highest interest, namely, the circumstance that the spectrum is
produced and the bodies recognized, however far from the observer the
luminous gas may be placed, the only condition required being that the
rays reach the instrument.
Until Kirchhoff and Bunsen’s spectroscopic investigations, lithium was
supposed to be a rare metal, occurring only in a few minerals. It happens
that this substance yields a remarkable spectrum (No. 4), for it gives an
extremely vivid line of a splendid red colour, accompanied by only one
other, a feeble yellow line; and the reaction is of very great delicacy, for
1 6000000 of a grain can easily be detected, and an eye which has once
seen the red line readily recognizes it again. A single drop of a mineral
water containing lithium has been found to distinctly produce the red line,
in cases where the quantity contained in a quart of the water would have
escaped ordinary chemical analysis. The spectroscope has shown that
lithium, so far from occurring in only four or five minerals, is a substance
very widely diffused in nature. In the waters of the ocean, in mineral and
river waters, in most plants, in wines, tea, coffee, milk, blood, and muscle,
this metal has been found. Dr. Roscoe states that the ash of a cigar, when
moistened with hydrochloric acid, and held in a platinum wire in the flame of
the Bunsen’s burner, at once shows the principal lines of sodium, potassium,
calcium, and lithium. Salts of lithium and of strontium both impart a rich
crimson tint to flames, and it is hardly possible to detect any difference in
these colours with the naked eye; but, as the reader may see on comparing
spectra No. 4 and No. 6, the prism makes a wide distinction.
Matter for a very interesting chapter in the history of prismatic analysis
has been furnished by the discovery of four new elements by means of the
426spectroscope. In 1860 Bunsen observed that the residue, after evaporation,
of a certain mineral water, yielded spectra with bright lines which
he had not seen before. He concluded that they were due to some unknown
elements, and, in order to separate these, he evaporated many tons
of the water, and was rewarded by the discovery of two alkaline metals,
cæsium and rubidium. The delicacy of the spectrum reaction may be
inferred from the fact of a ton weight of the water containing only three
grains of the salts of each of these substances. Rubidium gives a splendid
spectrum, containing red, yellow, and green lines, and also two characteristic
violet lines; while cæsium has orange, yellow, and green lines, and
two very beautiful blue lines, by which it is easily recognized.
About the same time, Mr. W. Crookes discovered, in a mineral from the
Hartz, another elementary body, the existence of which was first indicated
to him by the characteristic spectrum it produces, namely, a single splendid
green line (No. 8 spectrum). In 1864 two German chemists discovered,
also in the Hartz, a fourth new element, which was detected by two well-defined
lines in the more refrangible end of the spectrum—(see spectrum
No. 9, in the plate). This metal was named Indium, in reference to the
colour of its lines, and the names of the other three—cæsium, rubidium,
and thallium, are also derived from the colours of their characteristic lines.
Fig. 220.—Miniature Spectroscope.
Although the reader may, from such representations of the spectra as
those given in Plate XVII., form some idea of their appearance, he would
find his knowledge of the subject much clearer if he had the opportunity
of examining for himself the actual phenomena. We have already recommended
the performance of certain easy experiments involving no outlay,
but, in the matter of spectroscopes, carefully finished optical and mechanical
work is absolutely necessary in the appliances. It fortunately happens
that one eminent optician, at least, has made it his study to produce good
spectroscopic apparatus at the lowest possible cost, and if the reader be
interested in this subject, and desirous of trying experiments himself, he
can, for a very moderate sum, be equipped with all the appliances for
examining the phenomena we have described. He has only to procure, in
the first place, a small direct-vision spectroscope, such as that represented
of its actual size in Fig. 220, which is sold by Mr. Browning for twenty-two
shillings; secondly, a Bunsen’s burner, a few feet of india-rubber
tubing, two inches of platinum wire, and a few grains of the salts of lithium,
strontium, thallium, &c. The whole expense will probably be covered by
adding four shillings to the cost of the spectroscope, and the reader will
then be in a position to see for himself the principal Fraunhofer lines, the
spectra of the metals already referred to, and the absorption bands of the
427gases which have been mentioned, as well as the absorption bands in liquids
which will be spoken of in the sequel.
Fig. 221.—The Gassiot Spectroscope.
The splitting up of a beam of light into its elements—which it is the
office of the prism to produce—is accomplished by a single prism to a certain
degree only. It separates the red from the green, for example; but
the colours pass into each by insensible gradations through orange, yellow,
428and greenish yellow. If we allow the rays to fall upon a second prism after
emerging from the first, the separation is carried further; the red, for instance,
is spread out into different kinds of red, and so on with the rest.
And the greater the number of prisms, the greater is the extension which
is given to the spectrum. Now, just as by increasing the power of the telescope,
new stars become visible, whose light was before too faint, and
nebulæ, or stars which before seemed single, are resolved into clusters of
individual stars—so, by increasing the power of the spectroscope by employing
two, four, or more prisms, lines which appear single by the less
powerful instruments are, in some instances, resolved into groups of lines,
and new lines come into view, which before were too faint to show themselves.
For example, if we view the Fraunhofer lines through a spectroscope
like that in Fig. 220, but having two prisms instead of one, we shall
see that the D line is not really a single line, but is formed of two lines
close together. If we use greater dispersive power by employing a greater
number of prisms, we shall observe with solar light that when these two D
lines are sufficiently separated, several other lines make their appearance
between them. In this way the number of dark lines in sunlight, which
have been carefully mapped by Kirchhoff and others, amount to upwards
of 2,000; and no doubt there are many more lines waiting a still more
powerful instrument. Fig. 221 is copied from a large spectroscope made
by Mr. Browning for Mr. Gassiot. It has nine or more highly dispersive
glass prisms; the telescope and the tube bearing the slit have focal lengths
of 18 in., the lenses having a diameter of 1½ in.; the telescope is provided
with a slow motion for taking the angular position; and there is a third
tube provided with a micrometer, by which the position of the lines can be
measured to 1 10000th of an inch.
The instruments we have mentioned, except the miniature spectroscope,
show only a portion of the spectra at once, a movement of the telescope
being requisite to bring each part into view. It has been already stated
that the only position of the prism which will make the lines clear and
well defined is that in which the deviation is the least. In using trains of
prisms it is therefore necessary to adjust each prism for the part of the
spectrum which may be under observation. This is a tedious process, and
it has been obviated by a useful invention of Mr. Browning’s, by which the
adjustment is rendered automatic—that is, the movements of the telescope
are communicated to the prisms in such a manner that they place themselves
into the proper position for producing clear images of the slit, whatever
may be the refrangibility of the rays under examination: Fig. 222
shows the arrangement as it appears when viewed from above. The train of
six prisms can be so arranged that the ray after passing through six of them
shall be totally reflected by a surface of the last prism, and pursue again
its path through the six prisms in the reverse direction, becoming more
and more dispersed by each prism until it emerges parallel to the axis of
the telescope. The power of the instrument is, therefore, equivalent to
that of one with twelve prisms; but it can be used at pleasure with any
dispersive power, from two to twelve prisms.
Fig. 222.—Browning’s Automatic Adjustment of Prisms.
By making use of one of the Bunsen burners, the lines which are characteristic
of some ten or twelve metals are readily seen when one of their more
volatile salts is converted into vapour. For this purpose their chlorides
are usually employed, but the reactions are common to all their salts. It is
necessary that the metal should exist in the flame in the state of highly
heated vapour or gas, in order that its characteristic rays should be given
429off. We usually introduce compounds of these metals into the flame; but
there is reason to believe that these are decomposed in the flame, and the
disassociated metal takes the form of glowing gas, a small quantity of
which suffices for the production of the bright lines. No doubt the other
constituent of the compound, the chlorine for example, is also set free in
the gaseous form; but since the spectrum of the metal only is visible, we
may infer that at the temperature of the flame, the non-metallic elements
are not sufficiently luminous to produce a spectrum. When we repeat the
experiments with salts of the less volatile metals, we obtain no spectra—the
temperature of the flame not being sufficiently high to convert these
into vapour. Other methods have, therefore, to be resorted to, and advantage
is taken of the fact discovered by Faraday, that an electric spark is
nothing but highly heated matter. The spectroscope gives us reason to
believe that this matter, which is formed of the substances between which
the spark passes, is in the gaseous state; for it is found, on examining
sparks passing between two pieces of each metal, that characteristic bright
lines are produced. If one of the metals already named is submitted to
this examination, the same lines are found which are seen in the spectra
produced by the salts of the metal volatized in the flame, but in some cases
additional bright lines appear in the spark spectrum. With the heavier
metals the spark, or the electric arc, is, however, the only means of igniting
their vapours. The usual mode of doing this is to make the discharges of
a large induction coil pass between the two fine wires of the metals, placed
about a quarter of an inch apart. A Leyden jar is commonly employed to
condense the discharge, and thus produce a still higher temperature. Mr.
Browning has contrived the neat little apparatus shown in Fig. 223, in
which the jar is superseded by a more compact and convenient condenser
430inside of the box, so that it is only necessary to attach one terminal of the
coil to the binding-screw, seen outside of the end of the box, and place the
other wire from the coil in the binding-screw of one or the other of the
pieces of apparatus supported by the upright rod. Of these it is the one on
the right which at present engages our attention. Within a small glass
cylinder are two sliding rods, terminated by screw-clips, which hold finely-pointed
pieces of the metal under examination. The slit of the spectroscope
is placed close to the glass cylinder, and when a very rapid succession of
sparks is passing, the bright lines are seen continuously. The spectra of
metals examined in this way are found to yield a very large number of
lines. Thus the spectrum of calcium has 75 lines, and that of iron no fewer
than 450 lines. Our limits will not permit of an account of many interesting
particulars relating to these spectra, which include those of all the 50
metallic elements. It should, perhaps, be stated that a modified mode of
producing spectra by sparks is sometimes found useful. This consists in
causing sparks to pass between a solution of some salt of the metal and a
piece of platinum wire. The apparatus for this purpose is that shown on
the left side of the upright in Fig. 223.
Fig. 223.—Apparatus for Spark Spectra.
It remains to describe the method of producing spectra of the gaseous
non-metallic elements, such as oxygen, nitrogen, hydrogen, &c. For this
purpose electricity is again made use of. It has been found that while an
electric discharge cannot take place across a perfect vacuum, and air or
gas, at ordinary densities, offers much resistance to the passage of electricity,
on the other hand, a highly rarefied gas permits the discharge to
take place through it with great facility. This is seen in Geissler’s tubes,
where a succession of discharges from a Ruhmkorff’s coil causes the tubes
431to appear filled with light—due to the heating to incandescence of a very
minute quantity of the gas. The eye readily recognizes difference of colour
in the light given off by the different gases, and when this light is examined
by the spectroscope, bright lines, characteristic of each gas, are observed.
Nos. 12 and 13, in Plate XVII., are the spectra of hydrogen and of nitrogen
respectively, which appear when the gases are examined in the manner just
described. In this manner the spectra of chlorine, bromine, iodine, oxygen,
sulphur, phosphorus, &c., may be studied. Silicon and some other solid
non-metallic elements present great difficulties to the spectroscopist, for
these elements cannot be volatized at any temperature we can command,
and the spectra of their elements can only be inferred from those of their
compounds. But unfortunately the spectra are found to vary with the nature
of the compound, and thus it happens that in the case of carbon, for
example, no definite spectrum can be assigned to the element. The flame
of coal-gas, burning in the air, as in the Bunsen burner, gives the spectrum
No. 14; but if this is compared with the spectrum of the flame of burning
cyanogen (a compound of carbon and nitrogen), the two are found to differ
greatly. The cyanogen spectrum has the two pale broad bands of violet-blue,
the four blue lines, the two green lines, and the brightest of the greenish
yellow which are seen in the coal-gas spectrum. But it has in addition a
characteristic series of violet lines, a series of bright blue, two or three
crimson and red lines, and bands in the orange, and several green lines,
none of which occur in the coal-gas spectrum. These additional lines are
not due to nitrogen, for, with perhaps the exception of some red lines, they
do not coincide in position with any of the nitrogen lines. The spectrum
of hydrogen, No. 12, should be noticed, as its three lines are very distinct,
and it will be observed that they exactly coincide in their position with the
three Fraunhofer lines, C, F, and G, in No. 1.
There is another branch of this extensive subject to which we have now
to invite the reader’s attention. The power of certain gases to absorb or
stop certain rays of an otherwise continuous spectrum has already been
mentioned; but this property is by no means confined to gases, for certain
liquids and solids do this in a high degree. There is a remarkable metallic
element, named didymium. It is a rare substance, and its presence cannot
with certainty be detected by any ordinary tests. Its salts, however,
form solutions without colour, or nearly so, which have the power of strongly
absorbing certain rays. If we hold before the slit of the spectrum a small
tube containing a solution of any one of the salts, and allow the rays from
the sun, or from a luminous gas or candle-flame, to pass through it, we see
the spectrum crossed by certain well-defined very dark bands. A spectrum
of this kind is called an absorption spectrum, and the position, number,
width, &c., of dark bands are found to be as peculiar to each substance as
are the bright lines in the spectra of the elements. The method of observing
them when produced by solutions is very simple. The liquid is contained
in a small test-tube, which is placed in front of the slit; or, more conveniently,
the liquid is put into a wedge-shaped vessel, and thus the thickness
of the stratum of liquid through which the rays pass can easily be varied,
so that the best results may be obtained. The absorption spectra are produced
by many compound substances. A striking absorption spectrum is
seen when a solution in alcohol of the green colouring matter of leaves
(chlorophyll) is examined; for several distinct bands are seen, one in the red
being especially well marked. Many other coloured bodies exhibit characteristic
absorption bands, as, for example, permanganate of potash, uranic
432salts, madder, port wine, and magenta. The bands are so peculiar for each
substance, that if so-called port wine, for example, owe its colour to colouring
matter other than that of the grape, such as logwood, &c., the adulteration
can be instantly detected by a glance at the absorption spectrum. As, however,
the absorption bands are not, like the bright lines of metals, definite
images of the slit, but rather broad portions of the spectra, it is very desirable
in examining such spectra to compare them directly with those of
known substances, by throwing two spectra into one field, by means of a
side reflecting prism, as already described.
Perhaps one of the most interesting examples of absorption spectra is
that of blood. A single drop of blood in a tea-cupful of water will show
its characteristic spectrum when it is properly examined. If the blood is
arterial or oxidized blood, two well-marked dark bands are visible; but if
venous or deoxidized blood be used, we see, instead of the two dark bands,
a single one in an intermediate position. These differences have been
proved to be due to oxidization and deoxidization of a constituent of the
blood, called hæmoglobin, and by using appropriate chemical reagents, the
same specimen of blood may be made to exhibit any number of alternations
of the two spectra, according as oxidants or reducing reagents are employed.
It would be possible by an examination of the absorption spectrum
of a drop of arterial blood to pronounce that a person had died of suffocation
from the fumes of burning charcoal. In such case, the supply of oxygen
being cut off, the hæmoglobin of the whole of the blood in the system becomes
deoxidized.
The beautiful delicacy of these spectrum reactions has permitted the
spectroscope to be applied to the microscope with signal success by Mr.
Browning, working in conjunction with Mr. Sorby, who has devoted great
attention to this subject. The Sorby-Browning instrument is a direct-vision
spectroscope, with a slit, lens, &c., placed above the eye-piece of the microscope.
By receiving the light through a single drop of an absorptive liquid
placed under the object-glass of the microscope, the characteristic bands
are made visible. The micro-spectroscope is also a valuable instrument for
examining the absorption bands which are found in the light reflected from
solid bodies, for the smallest fragment suffices to fill the field of the microscope.
Mr. Sorby is able to obtain most unmistakably the dark bands
peculiar to blood from a particle of the matter of a blood-stain weighing
less than 1 1000th part of a grain. It is plain from this that the spectroscope
must sometimes prove of great service in giving evidence of crime from
traces which would escape all ordinary observation.
The micro-spectroscope, in its most complete form, is represented in
Fig. 224. As may be seen from the figure, the apparatus consists of several
parts. The prism is contained in a small tube, which can be removed at
pleasure; below the prism is an achromatic eye-piece, having an adjustable
slit between the two lenses; the upper lens being furnished with a
screw motion to focus the slit. A side slit, capable of adjustment, admits,
when required, a second beam of light from any object whose spectrum it
is desired to compare with that of the object placed on the stage of the
microscope. This second beam of light strikes against a very small prism
suitably placed inside the apparatus, and is reflected up through the compound
prism, forming a spectrum in the same field with that obtained from
the object on the stage. A is a brass tube carrying the compound direct-vision
prism, and has a sliding arrangement for roughly focussing.
433
Fig. 224.—The Sorby-Browning Micro-Spectroscope.
B, a milled head, with screw motion to finely adjust the focus of the
achromatic eye-lens.
C, milled head, with screw motion to open or shut the slit vertically.
Another screw, H, at right angles to C, regulates the slit horizontally. This
screw has a larger head, and when once recognized cannot be mistaken for
the other.
D D, an apparatus for holding a small tube, that the spectrum given by its
contents may be compared with that from any other object on the stage.
E, a screw, opening and shutting a slit to admit the quantity of light
required to form the second spectrum. Light entering the aperture near
E strikes against the right-angled prism which we have mentioned as being
placed inside the apparatus, and is reflected up through the slit belonging
to the compound prism. If any incandescent object is placed in a suitable
position with reference to the aperture, its spectrum will be obtained, and
will be seen on looking through it.
F shows the position of the field lens of the eye-piece.
G is a tube made to fit the microscope to which the instrument is applied.
To use this instrument, insert G like an eye-piece in the microscope tube.
Screw on to the microscope the object-glass required, and place the object
whose spectrum is to be viewed on the stage. Illuminate with stage mirror
if transparent, with mirror and lieberkühn and dark well if opaque, or by
side reflector, bull’s-eye, &c. Remove A, and open the slit by means of the
milled head, H, at right angles to D D. When the slit is sufficiently open
the rest of the apparatus acts like an ordinary eye-piece, and any object
can be focussed in the usual way. Having focussed the object, replace A,
434and gradually close the slit till a good spectrum is obtained. The spectrum
will be much improved by throwing the object a little out of focus.
Every part of the spectrum differs a little from adjacent parts in refrangibility,
and delicate bands or lines can only be brought out by accurately
focussing their own parts of the spectrum. This can be done by the milled
head, B. Disappointment will occur in any attempt at delicate investigation
if this direction is not carefully attended to. When the spectra of very
small objects are to be viewed, powers of from ½ in. to 1 20th, or higher,
may be employed. Blood, madder, aniline dyes, permanganate of potash
solution, are convenient substances to begin experiments with. Solutions
that are too strong are apt to give dark clouds instead of delicate absorption
bands. Small cells or tubes should be used to hold fluids for examination.
Mr. Browning has still further improved the micro-spectroscope by the
ingenious arrangement for measuring the positions of the lines, which is
represented in Fig. 225, and the construction and the use of which he thus
described in a paper read before the Microscopical Society:
Fig. 225.—Section of Micro-Spectroscope with Micrometer.
Attached to the side is a small tube,
A A. At the outer part of this tube
is a blackened glass plate, with a fine
clear white pointer in the centre of
the tube. The lens, C, which is focussed
by sliding the milled ring, M, produces
an image of the bright pointer
in the field of view by reflection from
the surface of the prism nearest the
eye. On turning the micrometer, M,
the slide which holds the glass plate
is made to travel in grooves, and the
fine pointer is made to traverse the
whole length of the spectrum.
It might at first sight appear as if
any ordinary spider’s web or parallel
wire micrometer might be used instead
of this contrivance. But on
closer attention it will be seen that
as the spectrum will not permit of
magnification by the use of lenses,
the line of such an ordinary micrometer
could not be brought to focus
and rendered visible. The bright
pointer of the new arrangement possesses
this great advantage—that it
does not illuminate the whole field
of view.
If a dark wire were used, the bright
diffused light would almost obscure
the faint light of the spectra, and entirely
prevent the possibility of seeing,
let alone measuring, the position of lines or bands in the most refrangible
part of the spectrum.
To produce good effects with this apparatus the upper surface of the
compound prism, P, must make an angle of exactly 45° with the sides of
435the tube. Under these circumstances the limits of correction for the path
of the rays in their passage through the dispersing prisms are very limited
and must be strictly observed. The usual method of correcting by the outer
surface is inadmissible. For the sake of simplicity, some of the work of
the lower part of the micro-spectroscope is omitted in the engraving. As
to the method of using this contrivance: With the apparatus just described,
measure the position of the principal Fraunhofer’s lines in the solar spectrum.
Let this be done carefully, in bright daylight. A little time given
to this measurement will not be thrown away, as it will not require to be
done again. Note down the numbers corresponding to the position of the
lines, and draw a spectrum from a scale of equal parts. About 3 in. will
be found long enough for this spectrum; but it may be made as much
longer as is thought desirable, as the measurements will not depend in any
way on the distance of these lines apart, but only on the micrometric numbers
attached to them. Let this scale be done on cardboard and preserved
for reference. Now measure the position of the dark bands in any absorption
spectra, taking care for this purpose to use lamplight, as daylight
will give, of course, the Fraunhofer lines, which will tend to confuse your
spectrum. If the few lines occurring in most absorption spectra be now
drawn to the same scale as the solar spectrum, on placing the scales side
by side, a glance will show the exact position of the bands in the spectrum
relatively to the Fraunhofer lines, which thus treated form a natural and
unchangeable scale (see diagram, Fig. 226). But for purposes of comparison
it will be found sufficient to compare the two lists of numbers representing
the micrometric measures, simply exchanging copies of the scale
of Fraunhofer lines, or the numbers representing them will enable observers
at a distance from each other to compare their results, or even to work
simultaneously on the same subject.
Fig. 226.
A simpler form of the micro-spectroscope is also made by Mr. Browning
at a very modest price, and if the reader possesses a microscope, and
desires to examine these interesting subjects for himself, he will do well to
procure this instrument, instead of that represented in Fig. 220, as it will
also answer better for other purposes. A section of the instrument is shown
in Fig. 227. When used with the microscope it is slipped into the place of
the eye-piece. There is an adjustable slit, a reflecting prism, by which two
different spectra may be examined at once, and a train of five prisms for
dispersing the rays. It can be used equally well for seeing the bright lines
436of metals and the Fraunhofer lines, and for viewing any two spectra simultaneously.
These direct-vision spectroscopes are better adapted for general
use by those who have not several different instruments, than such forms as
that shown in Fig. 229, for in the direct-vision instruments the whole extent
of the spectrum is visible at one view, which is by no means the case with
the larger instruments.
Fig. 227.—Section of Micro-Spectroscope.
We now approach that portion of our subject in which its interest culminates,
for however remarkable may be some of the above-named
results of this searching optical analysis, they are surpassed by those which
have been obtained in the field upon which we are about to enter. The
cause of the dark lines which Fraunhofer observed in the light of the sun
and of certain stars remained unexplained, he only establishing the fact that
they must be due to some absorptive power existing in the sun and stars
themselves, and not to anything in our atmosphere. It was reserved for
Professor Kirchhoff, of the University of Heidelberg, to show the full significance
of the dark lines. Fraunhofer had, on his first observation of the
lines, noticed that the D lines were coincident with the bright lines in the
spectrum of sodium. This interesting fact may be readily observed with
any spectroscope which permits of the two spectra being simultaneously
viewed. The bright line (or lines if the spectroscope be powerful) of the
metal is seen as a prolongation of the dark D solar line. Even with an
instrument like that shown in Fig. 220 the coincidence may be noticed.
Let the observer receive into the instrument the rays in diffused daylight
only, when he will still see the principal Fraunhofer lines distinctly, and
let him note the exact position of the D line, while he brings in front of the
slit the flame of a spirit-lamp charged with a little salt. He will then see
the bright yellow line replacing the dark D line, and by alternately removing
and putting back the lamp he will be soon convinced of the perfectly identical
position of the lines.
This fact remained without explanation from 1814 to 1859, when Kirchhoff
accidentally found, to his surprise, that the dark D line could be produced
437artificially. He says: “In order to test in the most direct manner possible
the frequently asserted fact of the coincidence of the sodium lines with the
D lines, I obtained a tolerably bright solar spectrum, and brought a flame
coloured by sodium vapour in front of the slit. I then saw the dark lines
D, change into bright ones. The flame of a Bunsen’s lamp threw the bright
sodium lines upon the solar spectrum with unexpected brilliancy. In order
to find out the extent to which the intensity of the solar spectrum could be
increased without impairing the distinctness of the sodium lines, I allowed
the full sunlight to shine through the sodium flame, and, to my astonishment,
I saw that the dark lines, D, appeared with an extraordinary degree
of clearness. I then exchanged the sunlight for the Drummond’s or oxy-hydrogen
lime-light, which, like that of all incandescent solid or liquid
bodies, gives a spectrum containing no dark lines. When this light was
allowed to fall through a suitable flame, coloured by common salt, dark
lines were seen in the spectrum in the position of the sodium lines. The
same phenomenon was observed if, instead of the incandescent lime, a
platinum wire was used, which, being heated in the flame, was brought to
a temperature near its melting point, by passing an electric current through
it. The phenomenon in question is easily explained, upon the supposition
that the sodium flame absorbs rays of the same degree of refrangibility
as those it emits, whilst it is perfectly transparent for all other rays.”
(Quoted in Roscoe’s Lectures on “Spectrum Analysis.”) When the light
of ignited lime was similarly made to pass through flames containing the
incandescent vapours of potassium, barium, strontium, &c., the bright lines
which these substances would have produced had the lime-light not been
present were found to be in every case changed into dark lines, occupying
the very same positions in the spectrum. In such experiments the flames
containing the metals in the vapourized state do all the time really give
off those rays which are peculiar to each substance; but when a more
intense illumination—such as the lime-light, the electric arc, or direct
sunlight—passes through them, the rays of the spectrum produced by the
intense light overpower those given off by the relatively feebly coloured
flames, and hence the portions of the spectrum which are occupied by
these, appear black. But as the intense light would give a perfectly continuous
spectrum if the incandescent metallic vapour allowed the rays
corresponding to its lines to pass through it, the inference is obvious that
each vapour absorbs those particular rays which it has itself the power of
emitting, but allows all others to pass freely through it. Besides the experimental
proofs of this fact which have been already adduced, many others
might be named. The flame of a spirit-lamp with a salted wick appears
opaque and smoky when we look through it at a large flame of burning
hydrogen, also coloured by sodium; for the rays emitted by the latter do
not penetrate the former, which, in consequence of its feebler light, appears
dark by comparison. Again, if an exhausted tube containing metallic
sodium be heated so as to convert the sodium into vapour, the tube viewed
by the light of a sodium flame appear to contain a black smoke, and the
light from the flame will no more pass through it than through a solid
object; yet the tube appears perfectly transparent when viewed by ordinary
light, and the light from a lithium or other coloured flame would also
pass freely. Kirchhoff was led by purely theoretical reasoning to conclude
that all luminous bodies have precisely the same power of absorbing certain
rays of light as they have of emitting them at the same temperature, and
he thus brought luminous rays under the same general law which had
438previously been established for radiant heat by Prevost, Dessains, Balfour
Stewart, and others. Here, then, a law was arrived at, and, abundantly
confirmed by direct experiment as regards the more volatile metals, it
was ready to supply the most satisfactory explanation of the coincidences
which were everywhere discovered to exist between the Fraunhofer lines
and those which belong to terrestrial substances. For Kirchhoff also
found, when mapping the very numerous lines seen in the spark spectrum
of iron, that for each of the 90 bright lines of iron which he then observed,
there was a dark line in the solar spectrum exactly corresponding in position.
The number of observed bright lines in the iron spectrum has been
since extended to 460, and yet each is found to have its exact counterpart
in a solar dark line.
So many coincidences as these made it certain that these dark lines and
the bright lines of iron must have a common cause, for the chances against
the supposition that the agreement was merely accidental are enormous.
Kirchhoff actually calculated, by the theory of probabilities, the odds against
the supposition. He found it represented by 1,000,000,000,000,000,000 to 1.
The result arrived at in the case of sodium at once suggested the explanation
that these lines were produced by an absorptive effect of the vapour
of iron. Now, the existence of such a vapour in our atmosphere could not
be admitted, while the temperature of the sun was known to be exceedingly
high, far higher, indeed, than any temperature we can produce by electricity,
or any other means. Hence, Kirchhoff concluded that his observations
proved the presence of the vapour of iron in the sun’s atmosphere
with as much certainty as if the iron had been actually submitted to chemical
tests. By the same reasoning, Kirchhoff also demonstrated the existence
in the solar atmosphere of calcium, chromium, magnesium, nickel, barium,
copper, and zinc. To these, other observers have added strontium, cadmium,
cobalt, manganese, lead, potassium, aluminium, titanium, uranium,
and hydrogen. It has also been demonstrated that a considerable number
of the Fraunhofer lines are due to absorption in our atmosphere by its gases
and aqueous vapour. This demonstration of the existence of iron and
nickel in the sun is an interesting pendent to the known composition of
many meteorites which reach us from interplanetary space.
Kirchhoff was led to believe that the central part of the sun is formed of
an incandescent solid or liquid, giving out rays of all refrangibility, just as
white-hot carbon does; that round this there is an immense atmosphere,
in which sodium, iron, aluminium, &c., exist in the state of gas, where they
have the power of absorbing certain rays; that the solar atmosphere extends
far beyond the sun, and forms the corona; and that the dark sunspots,
which astronomers have supposed to be cavities, are a kind of cloud,
floating in the vaporous atmosphere.
During total eclipses of the sun, certain red-coloured prominences have
been noticed projecting from the sun’s limb, and visible only when the glare
of its disc is entirely intercepted by the moon. Fig. 228 represents a total
eclipse, and will give a rude notion of the appearance of the red prominences
seen against the fainter light of the corona, which extends to a considerable
distance beyond the sun’s disc. Now, two distinguished men of science
simultaneously and independently made the discovery of a mode of seeing
these red prominences, even when the sun was unobscured. M. Janssen
was observing a total eclipse of the sun in India, and the examination by
the spectroscope of the light emitted from the red prominences showed
him that they were due to immense columns of incandescent hydrogen, for
439he recognised the red line and blue lines which belong to the spectrum of
this gas (see No. 12, Plate XVII.). Mr. Norman Lockyer at the same time
also succeeded in viewing the solar prominences in London without an
eclipse. He found a red line perfectly
coinciding in position with
Fraunhofer’s C line and that of hydrogen,
another nearly coinciding
with F, and a third yellow line near
D. Soon after this, Dr. Huggins discovered
a mode of observing the
shape of the red prominences at any
time, by using a powerful train of
prisms and a wide slit, so that the
changes in the forms of the red
flames can be followed. Now, since
the red prominences give off only a
few rays of particular refrangibility,
it is not difficult to understand that
the light of the sun might be, as it
were, so diluted by stretching out
the spectrum, by means of a train of
many prisms, that almost only the red
rays, C, should enter the telescope,
and occupy the field with sufficient
intensity to overpower all others, and produce an image of the object from
which they originated. The nature of this action may be illustrated thus: If
we hold vertically a prism, and look through it at a candle-flame, we may perceive
a lengthened-out image of the flame, showing the succession of prismatic
colours, and formed, as it were, of a red image of the flame close to a
yellow one, and so on, but presenting no defined form. If, still viewing this
spectrum, we introduce into the flame on a platinum wire a piece of common
salt, we shall perceive a well-defined yellow image of the candle start out,
because the rays which are emitted by the incandescent sodium, being all
of one refrangibility, the prism simply refracts without dispersing them.
The dispersion which weakens the light of the continuous spectrum by
lengthening it out, does not sensibly detract from the brilliancy of the bright
lines, as their breadth is scarcely increased—they are refracted but not dispersed.
Hence, when a sufficient number of prisms is employed, the bright
lines of the solar chromosphere may be seen in full sunshine, in spite of the
greater intensity of the light emanating from the photosphere, which produces
the continuous spectrum. The bright C line is, of course, a virtual
image of the slit produced by rays of that particular refrangibility; but by
using a very high dispersive power, the slit may be opened so wide that the
C rays form in the telescope a red image of the prominence from which they
issue, since their light will predominate over that of any rays belonging to
the continuous spectrum.
Fig. 228.—Solar Eclipse, 1869.
In the hands of Mr. Norman Lockyer the science of the physical and
chemical constitution of the sun has made rapid progress, and new facts
are continually being observed, which serve to furnish more and more definite
views. Mr. Lockyer considers that, extending to a great distance around
the sun is an atmosphere of comparatively cooler hydrogen, or perhaps of
some still lighter substance which is unknown to us. It is this which forms
what is termed the corona, or circle of light which is seen surrounding the
440sun in a total eclipse. Immersed in this, and extending to a much smaller
distance from the nucleus of the sun, is another envelope, termed the chromosphere,
consisting of incandescent hydrogen and some glowing vapours of
magnesium and calcium. The brightest part of this envelope, which lies
nearest the sun, is that which gives off the red rays by which the prominences
may be observed without an eclipse. These prominences have been
shown to be tremendous outbursts of glowing hydrogen, belched up with
sometimes an enormous velocity from below, since they have been observed
to spring up 90,000 miles in a few minutes. Beneath the chromosphere,
and nearer to the body of the sun, are enormous quantities of the vapours
of the different elements—sodium, iron, &c.—to which the dark lines of the
solar spectrum are due. This stratum Mr. Lockyer calls the reversing layer,
because it reverses (turns to dark) the lines which would otherwise have
appeared bright, just as Kirchhoff’s sodium vapour did in the experiment
described on page 437. Beneath the reversing layer is the photosphere, from
which emanates the light that is absorbed in part by the reversing layer,
and which there is good reason to believe is either intensely heated solid
or liquid matter.
In 1861 Dr. Huggins devoted himself, with an ardour which has since
known no remission, to the extension of prismatic analysis to the other
heavenly bodies. The difficulties of the investigations were great. There
was first the small quantity of light which a star sends to the spectator;
this was obviated by the use of a telescope of large aperture, which admitted
and brought to a focus many more rays from the star, and therefore
the brightness of the image was proportionately increased. Not so the
size of the image: the case of the fixed stars for this always remains a
mere point. It was, of course, necessary to drive the telescope by clockwork,
so that the light of the star might be stationary on the field of the
spectroscope. As the spectrum of the image of the star formed by the
object-glass would be a mere line, without sufficient breadth for an observation
of the dark or light lines by which it might be crossed, it is necessary
to spread out the image so that the whole of the light may be drawn
out into a very narrow line, having a length no greater than will produce
a spectrum broad enough for the eye to distinguish the lines in it. This
is accomplished by means of a cylindrical lens placed in the focus of the
object-glass, and immediately in front of the slit. Covering one-half of
the slit is a right-angled prism by which the light to be compared with that
of the star is reflected into the slit. The light is usually that produced
by taking electric sparks between wires of the metal in the manner already
described. The dispersive power of the spectroscope was furnished by two
prisms of very dense glass, and the spectrum was viewed through a telescope
of short focal length. Dr. Huggins’s observations lead him to the
conclusion that the planets Mars, Jupiter, and Saturn possess atmospheres,
as does also the beautiful ring by which Saturn is surrounded; for he
noticed in the spectrum of each different dark lines not belonging to the
solar spectrum.
Fig. 229.—The Planet Saturn.
Passing to the results obtained in the case of the fixed stars, we may
remind the reader of the enormous distance of the bodies which are submitted
to the new method of analysis. Sir John Herschel gives the following
illustration of the remoteness of Sirius—supposed to be one of the
nearest of the fixed stars: Take a globe, 2 ft. in diameter, to represent the
sun, and at a distance of 215 ft. place a pea, to give the proportionate size
and distance of the earth. If you wish to represent the distance of Sirius
441on the same scale, you must suppose something placed forty thousand
miles away from the little models of sun and earth. But not only do we
know with certainty some of the substances contained in Sirius, but the
star spectroscope has taught us a great deal about orbs so remote, that
their distance is absolutely unmeasurable. About Aldebaran we know
that there are hydrogen gas and vapours of magnesium, iron, calcium,
sodium, and some four or five other elements. Generally the lines indicate
the presence of hydrogen in these distant suns; but there is, at least, one
remarkable exception in αOrionis, the spectrum of which yields no trace
of the hydrogen lines, although it is evident that magnesium, sodium,
calcium, &c., are present. The spectra of celestial bodies are of several
kinds. Many of the stars have, like our sun, a continuous spectrum crossed
by dark lines. Such is that of Sirius, No. 10, Plate XVII. Others have,
however, both dark and bright lines, and some are marked by only three
bright spaces. Of the spectra of the nebulæ some have three bright lines
(see No. 11, Plate XVII.), and the bodies producing them are, therefore, to
be considered as masses of incandescent gas, while some give continuous
spectra. One of the bright lines in the spectra of the nebulæ coincides
with one of the hydrogen lines, and another—the brightest of the three—with
one of the brightest nitrogen lines; but the third does not agree with
any with which it has as yet been compared. The inference from these
appearances is that the nebulæ contain hydrogen and nitrogen, but the
absence of the other lines of these substances has not been fully explained;
although the observation of Dr. Huggins, that when the light of incandescent
nitrogen and hydrogen is gradually obscured by interposing layers
of neutral tinted glass, the lines corresponding with those in the nebular
442spectra are the last to disappear, seems to suggest a probable solution of
the difficulty.
Fig. 230.—Solar Prominences, No. 1.
There is another very interesting line of spectroscopic research in the
power the prism gives us of estimating the velocity with which the distances
of the stars from our system are increasing or diminishing. On closely
examining the hydrogen lines of Sirius, and comparing them with the bright
lines of hydrogen rendered incandescent by electric discharges in a Geissler
tube, the spectrum of which his instrument enabled him to place side by
side with that of the star, Mr. Huggins was surprised to find that the lines
in the latter did not exactly coincide in position with those of the former,
but appeared slightly nearer the red end of the spectrum. This indicated
a longer wave-length, or increased period of vibration, according to the
theory of light, which would be accounted for by a receding motion between
Sirius and the earth, just as the crest of successive waves of the sea would
overtake a boat going in the same direction at longer intervals of time than
those at which they would pass a fixed point, while, if the boat were meeting
the waves, these intervals would, on the other hand, be shorter. Hence
if the position of the lines in the spectrum depends on the periods of vibration,
that position will be shifted towards the red end when the luminous
body is receding from the earth with a velocity comparable to that of light,
and towards the violet end when the motion is one of approach. The change
in refrangibility observed by Mr. Huggins corresponded with a receding
velocity of 41·4 miles per second, and when from this was subtracted the
known speed with which the earth’s motion round the sun was carrying us
from the star at the time, the remainder expressed a motion of recession
443amounting to about twenty miles a second, which motion, there is reason
to believe, is chiefly due to a proper movement of Sirius. These deductions
from prismatic observations are of the highest value astronomically,
since they will eventually enable the real motions of the stars to be determined,
for ordinary observation could only show us that component of the
motion which is at right angles to the visual ray, while this gives the component
along the visual ray. In the same manner, it is inferred that Arcturus,
a bright star in the constellation Boötes, is approaching us with a
velocity of fifty-five miles per second.
Fig. 231.—Solar Prominences, No. 2.
When the solar spots are examined with the spectroscope, the dark image
of the slit produced by the hydrogen line, F, is observed to show a strange
crookedness when it is formed by rays from different parts of the spot.
This distortion is due to the same cause as the displacement of the stellar
lines, namely, motions of approach or recession of the masses of glowing
hydrogen. Mr. Norman Lockyer, to whom we are indebted for the most
elaborate investigations of the solar surface, has calculated, from the position
of the lines, the velocities with which masses of heated hydrogen are
seen bursting upwards, and those which belong to the down-rushes of cooler
gas. Velocities as great as 100 miles per second were, in this way, inferred
to occur in some of the storms which agitate the solar surface. Two drawings
of a solar storm, given by Mr. Lockyer, are shown in Figs. 230 and
231. These are representations of one of the so-called red prominences,
the first giving its appearance at five minutes past eleven on the morning
of March 14th, 1869, and the last showing the same ten minutes afterwards.
444The enormous velocity which these rapid changes imply will be
understood when it is stated that this prominence was 27,000 miles high.
“This will give you some idea,” says Mr. Lockyer, “of the indications which
the spectroscope reveals to us, of the enormous forces at work in the sun,
merely as representing the stars, for everything we have to say about the
sun the prism tells us—and it was the first to tell us—we must assume to
be said about the stars. I have little doubt that, as time rolls on, the spectroscope
will become, in fact, almost the pocket companion of every one
amongst us; and it is utterly impossible to foresee what depths of space
will not in time be gauged and completely investigated by this new method
of research.”
The light of comets has also been examined by the spectroscope, and
many interesting results arrived at. Our limits do not, however, permit
us to enter into a discussion of these interesting subjects.
Fig. 232 is a section of another of Mr. Browning’s popular instruments,
which is named by him the “Amateur’s Star Spectroscope.” It exhibits
very distinctly the different spectra of the various stars, nebulæ, comets, &c.
Fig. 232.—Section of Amateur’s Star Spectroscope.
The reader who is desirous of learning more of this fascinating subject
is referred to Dr. Roscoe’s elegant volume, entitled, “Lectures on Spectrum
Analysis.” This work, which is embellished with handsome engravings
and illustrated by coloured maps and spectra, gives a clear and full account
of every department of the subject, and in the form of appendices, abstracts
of the more important original papers are supplied, while a complete list
is given of all the memoirs and publications relating to the spectroscope
which have been published.
This brief account of the spectroscope and its revelations, which is all
that our space permits us to give, will not fail to awaken new thoughts in
the mind of a reader who has obtained even a glimpse of the nature of the
subject, especially in relation to that branch of which we have last treated,
for in every age and in every region the stars have attracted the gaze and
excited the imagination of men. The belief in their influence over human
affairs was profound, universal, and enduring; for it survived the dawn of
rising science, being among the last shades of the long night of superstition
which melted away in the morning of true knowledge. Even Francis
Bacon, the father of the inductive philosophy, and old Sir Thomas Browne,
the exposer of “Vulgar Errors,” believed in the influences of the stars; for
while recognizing the impostures practised by its professors, they still regarded
astrology as a science not altogether vain. It was reserved for the
mighty genius of Newton to prove that in very truth there are invisible
ties connecting our earth with those remote and brilliant bodies—ties more
potent than ever astrology divined; for he showed that even the most distant
orb is bound to its companions and to our planet by the same power
445that draws the projected stone to the ground. And now the spectroscope
is revealing other lines of connection, and showing that not gravitation alone
is the sympathetic bond which unites our globe to the celestial orbs, but
that there exists the closer tie of a common constitution, for they are all
made of the same matter, obeying the same physical and chemical laws
which belong to it on the earth. We learn that hydrogen, and magnesium,
and iron, and other familiar substances, exist in these inconceivably distant
suns, and there exhibit the identical properties which characterize them
here. We confirm, by the spectroscope, the fact partially revealed by other
lines of research, that the stars which appear so fixed, are, in reality, careering
through space, each with its proper motion. We learn also that the
stars are the theatres of vast chemical and physical changes and transformations,
the rapidity and extent of which we can hardly conceive. There
is, for example, the case of that wonderful star in the constellation of the
Crown, which, in 1866, suddenly blazed out, from a scarcely discernible
telescopic star, to become one of the most conspicuous in the heavens, and
the bright lines its beams produced in the spectroscope revealed the fact
that this abrupt splendour was due to masses—who can imagine how vast?—of
incandescent hydrogen. This brightness soon waned, and τCoronæ
Borealis reverted once more to all but telescopic invisibility. The seeming
fixity of the stars is an illusion of the same nature as that which prevents
a casual observer from recognizing their apparent diurnal motion, and now
we have also ample evidence that permanence of physical condition, even
in the stars, is impossible. Everywhere in the universe there is motion and
change; there is no pause, no rest, but a continual unfolding, an endless
progression.
“Know the stars yonder,
The stars everlasting,
Are fugitive also,
And emulate, vaulted,
The lambent heat-lightning
And fire-fly’s flight.”
ROENTGEN’S X RAYS.
Fig. 232a.—Living Hand. Exposure, 4 Minutes.
On page 507 reference will be made to certain remarkable effects observed
by Mr. Crookes when the electric discharges from an induction
coil are passed through very highly exhausted tubes. These phosphorescent
and mechanical effects Mr. Crookes attributed to streams
of “radiant matter” shot off from the negative pole with immense
velocities—the matter not being that of the electrode itself, but particles
of the extremely rarefied residual gas, which, being comparatively few,
could mostly traverse the tube in straight lines without coming into collision
446with their fellows, and thus a class of phenomena, different from
the striated discharges in the ordinary and less highly exhausted Geissler
tubes, comes into view. The emanations from the negative pole, or
cathode, in highly rarefied gases became known as the “cathode rays,”
and they began to be further examined by other observers, and more
particularly in 1894 by Hittorf, and by M. Lenard, a Hungarian physicist,
who found that they pass through thin plates of metal, and through wood
and other substances not transparent to ordinary light. It was also observed
by Lenard, and also previously by Hertz, that there are several
kinds of cathode rays, which differ from each other as regards their
powers of exciting phosphorescence, capability of being deflected by a
magnet, and the degrees in which they are absorbed by various media.
But universal attention was drawn to this subject by the announcement,
at the end of 1895, of certain discoveries made by Dr. W. K. Roentgen,
a professor of physics at Wurzburg. He covered a highly-exhausted
Crookes’ tube with black cardboard, and found that when the discharge
of a large induction coil was passed through the tube in a dark room, a
piece of paper coated on one side with platino-cyanide of barium, and
held near the covered tube, glowed with a brilliant fluorescence, no
447matter which side of the paper was turned towards the tube; and even at
a distance of two yards some fluorescence was still visible. On experimenting
with various bodies interposed between the covered tube and the
fluorescent screen, it was found that the emanations passed through nearly
every substance with more or less facility. The screen lit up when placed
behind a book of a thousand pages, also behind two packs of cards. A
single layer of tin-foil scarcely threw a shadow, and several thicknesses
were required to produce a distinct effect. Deal boards, an inch thick,
offered little resistance. A very thick plate of aluminium (6 10 inch) reduced
the fluorescence, but still allowed some rays to pass. The hand
held before the fluorescent screen showed a dark shadow of the bones
only, with but a faint outline of their fleshy investment. Copper, silver,
gold, platinum, and lead, in comparatively small thicknesses, intercept
these rays. Thus a plate of lead only five hundredths of an inch thick
almost stops them. Increase of thickness increases the resistance to their
passage in all cases; but the comparative transparency of a body cannot
be deduced from its thickness and density. Many other bodies besides
platino-cyanide of barium become fluorescent under the influence of these
rays, such as certain kinds of glass, Iceland spar, rock-salt, etc. Dr.
Roentgen is convinced that these rays are not the cathode rays or any
part of them; but as the theoretical nature of the new rays has not yet
been explained, he has preferred to provisionally call them the X rays, a
denomination doubtless suggested by the use of the symbol x in algebra
to represent unknown quantities.
The source of the X rays, Roentgen states, is at the place where the
cathode rays strike the walls of the exhausted tube, and produce the most
brilliant phosphorescence; but they cannot be cathode rays which have
merely passed through the glass, for, contrary to what has been observed
with respect to the latter, they cannot be deflected by a magnet. Nor is
glass the only substance in which they can be generated, for they were
obtained from an apparatus in which the cathode rays were made to impinge
upon a plate of aluminium nearly one-tenth of an inch thick.
Photographic dry plates are also sensitive to the X rays, and their power
to pass through wood, ebonite, etc., makes the experiments of testing the
opacity, or otherwise, of various objects for them quite easy. It is
necessary merely to place the object on the closed cover of the dark slide,
and place the whole under the vacuum tube; all the exposure, which is
somewhat prolonged in most cases, may be made in ordinary light. But
the light-tight boxes, in which photographic plates are packed, cannot,
of course, be brought near the apparatus, as they are completely permeable
to the X rays, and their whole contents may be rendered useless.
The impression obtained on the photographic plate is not so much a
photograph as a shadow of the interposed object—a shadow more or less
dense in the positive print according to the permeability of the object,
and the length of the exposure. These photographic results have sometimes
been called “shadowgrams,” “radiograms,” “radiographs,”
“skiagraphs,” etc. The word skiagraph appears the most appropriate
designation. That the emanations from the phosphorescing substance
on which the cathode rays impinge are entitled to be also called rays,
appears from the regularity of the shadows thrown on the fluorescent
screen or photographic plate; and the fact of their propagation in straight
lines was proved by Dr. Roentgen obtaining a pin-hole photograph of the
phosphorescing part of the vacuum tube, when the latter was enveloped
448in black paper. Why a pin-hole and not a lens was used for taking this
photograph will presently appear.
Fig. 232b.—Skiagraph of a Hand, by Dr. Roentgen. The Third Finger has a Ring on it.
One of Dr. Roentgen’s experiments excited the attention and interest
of the general public, as well as of the scientific world, in the most extraordinary
degree, and though its announcement was received in some
quarters with incredulity, experimenters in all parts of the world immediately
set themselves at work to test the truth of the alleged discovery.
Electrical apparatus of different kinds, with various adjustments, were
employed, with results that were in some cases failures, in others confirmations
of the German professor’s statements, and not unfrequently the
variations in the conditions gave rise to increased knowledge of the
phenomena generally. The experiment just alluded was one in which a
dry photographic plate contained in one of the camera dark slides, now
so familiar to every one, was placed (with the slide still closed by its
wooden cover of nearly one quarter of an inch thick) a few inches below
the Crookes’ tube, and the hand of a living-person being extended on the
outside of the cover, a shadow of the bones of the hand, as if seen through
the surrounding tissues, was obtained. Much popular misconception as
to the powers of the “new photography” arose from want of knowledge
of the process by which these strange pictures were obtained, the common
notion being that these photographs were produced by some method of
using a camera, and that outlines of people’s bodies and skeletons could
be taken instantaneously, not only through their clothes, but through
doors and walls. Much nearer the mark was the allusion of a scientific
writer as to the possibility of the new process realising Dickens’ description
449of Marley’s ghost: “His body was transparent, so that Scrooge, observing
him, and looking through his waistcoat, could see the two buttons
on his coat behind.” The value of the new discovery for medical and
surgical purposes was immediately recognised, and very soon its application
was successfully practised.
Dr. Roentgen found that the X rays are incapable of refraction, in this
respect differing from ordinary light (see pages 397 and following), and
among the experiments which most impressed and astonished his auditors
when he was lecturing at Potsdam on his new discovery before the
Imperial Court of Germany, was one in which he showed the X rays
passing in a straight line through water without undergoing refraction.
The rays pass without interruption equally through the substances,
whether these be coherent or in a layer of fine powder of the same thickness,
and this again shows that there can be no regular reflection or refraction.
Prisms and lenses, whether of glass, ebonite, or aluminium,
fail to afford evidence of refractive action, hence the X rays cannot be
focused like those of ordinary light, and that is why the photograph of
the vacuum tube had to be taken by a pin-hole. Again, glass lenses
could not be used, because this substance, so transparent to light, is particularly
opaque to the X rays, and would in a great degree intercept
them, while lenses of ebonite and of aluminium, which were tried, were
inoperative on account of the irrefrangibility of the rays.
As to the nature of the rays themselves, Dr. Roentgen rejects the notion
of their being “ultra-violet” rays, which was suggested by some. The
meaning of this term is seen when it is understood that a great distance
beyond the violet end of the visible spectrum there are radiations, revealed
by their photographic impressions, so that the whole spectrum is
really some eight times as long as the visible part. In consequence of
these ultra-violet rays acting on the photographic plate, it is possible, as
has long been known, to take a photograph in the dark. The eye is quite
insensible to the X rays also, and although these, as we have seen, readily
pass through the bodily tissues, it may be placed quite near the discharge
tube, the latter being enveloped in black paper, without causing any
sensation. That the new rays are in some way allied to light is the
opinion held by Dr. Roentgen, and he is inclined to consider them as due
to longitudinal vibrations in the ether; that is, instead of the transverse
waves to which light is attributed, these resemble the waves of sound, in
so far that they move in the direction of propagation. This would account
for the absence of any distinct refraction, or polarisation, which seems to
characterise the X rays. Their connection with certain electric Maxwell-Hertz
waves (see p. 541) is more problematical, as the mathematical
formulæ for these admit only transverse oscillation. But on the assumption
of certain conditions, due to the action of electricity, etc., on highly
rarefied air, the possible existence of longitudinal vibrations has been deduced
by admitting a certain variation in some of the factors of the Maxwell
formulæ.
Other suggestions have been advanced in order to make the observed
facts concerning the X rays fit into established theories, but so far these
attempts have been unsuccessful. It would seem as if our present conceptions
of light, electricity, the ether and matter, will have to be profoundly
modified and enlarged in order to bring these and other recently
discovered phenomena within their scope. Since the publication of Dr.
Roentgen’s paper, his results have received confirmation in every quarter,
450and many new observations have been added, some of which seem to
tend not so much to elucidate the phenomena, as to prove them even more
complicated than was at first supposed. Such was the announcement in
June, 1896, of the discovery of several varieties of X rays.
Fig. 232c.—Metal Objects taken through Calico and Sheet of Aluminium.
In the meantime, various modifications have been made in the forms of
the tubes and electrodes, and divers arrangements have been used for the
exciting electrical apparatus. Thus it has been found that the X rays
are given off from platinum more copiously than from glass, aluminium,
or any other substance, and by using a tube closed by a “platinum
window,” on which the cathode rays impinge, Mr. Gifford has been able
to reduce the time of exposure for obtaining a skiagraph of the bones
on the hand to half a minute, whereas twenty times that period was
formerly required. Another form of tube is advertised by Brady &
Martin of Newcastle, with which, in conjunction with a new screen, a
coil giving a 5–inch spark will, it is stated, yield a good skiagraph of the
hand in two seconds, which appears to be the shortest time yet attained.
Another firm of tube-makers, Newton & Co., London, state that their
special form of tube, excited by a coil giving a 6–inch spark, and used with
their fluorescent screen, “will work right through the human body, showing
the heart, liver, spine, ribs, the movements of the heart and of the
451diaphragm, etc.” It has recently been observed that the best results are
obtained when there is a certain, but as yet undefined, relation between
the degree of rarefaction of the residual gas in the tube, and the intensity
or frequency of the electric discharges, and that these should be accommodated
to the work required. Thus, for example, if a skiagraph of the
hand be attempted with an apparatus in which these factors are carried
to too high a degree, the resulting X rays will pass through the bones
almost as freely as through the surrounding tissues, and their shadows
will therefore not appear. If, on the other hand, the contrary conditions
hold, an incomplete or maybe no result will be found. This seems to
explain the failures that have sometimes occurred when tubes of apparently
identical construction have been used in the hands of the same, or
of different, observers. Perhaps more depends also on the time of exposure.
For instance, if a short exposure be given in the case of the hand,
the photograph will be merely a silhouette of that member; with a little
longer exposure, this will show the nails; with still longer time, the
shadow of the fleshy parts begins to grow faint and the skeleton to appear.
With yet more prolonged exposure only the bones will show, in their
various degrees of opacity, and the shadows of these will gradually disappear
as the time of exposure is increased, until at length the image will
be entirely effaced. The considerable differences as to distinctness of the
various tissues, which are exhibited by the published prints of hand
shadows, are thus explicable.
Fig. 232d.—A Skiagraph of Layers of Various Substances.
452
Fig. 233.—Portrait of Professor Helmholtz.
SIGHT. — THE EYE. — VISUAL IMPRESSIONS .
The investigations of modern science have borne rich fruit, not only by
vastly extending our knowledge of the universe of things around us,
but also making us acquainted with the mode in which certain agents act
upon our bodily organs, and by revealing, up to a certain point, what may
be termed the mechanism of that most wonderful thing—the human mind—or,
at least, that part which is immediately concerned in the perceptions
of an external world. Of all the physical influences which affect the human
mind, those due to light are the most powerful and the most agreeable.
One of the most ancient of philosophers says, in the simple words which
are appropriate to the expression of an undeniable truth, “Truly the light
is sweet, and a pleasant thing it is for the eyes to behold the sun.” The
impression produced by light alone is a source of pleasure—a cheering influence
of the highest order; and there is a special character in the pleasing
effects of light, from the circumstance that they do not exhaust the sense
so quickly as do even pleasurable impressions on other organs—such as
sweet tastes, fragrant odours, or agreeable sounds. Sight is not liable
to that satiety which soon overtakes the enjoyment of sensations arising
453from the other senses; it possesses, therefore, a refinement of quality of
which the rest are devoid. Sight converses with its objects at a greater
distance than does any other sense, and it furnishes our minds with a
greater variety of ideas. Indeed, our mental imagery is most largely made
up of reminiscences of visual impressions; for when the idea of anything
is brought up in our minds by a word, for example, there arises, in most
cases, a more or less vivid presentation of some visible appearance. Our
visual impressions are also longer retained in memory or idea than any
other class of sensations.
The nature of the impressions we receive through the eye is extremely
varied; for we thus perceive not only the difference between light and
darkness, but in the sensations of colour we have quite another class of
effects, while the lustre and sparkle of polished and brilliant objects add
new elements of beauty and variety. We find examples of the latter
qualities in the verdant sheen of the smooth leaf, in the splendid reflections
of burnished gold, in the bright radiance of glittering gems, and “in
gloss of satin and glimmer of pearls.” The eye is also the organ which
conveys to our minds the impressions of visible motion, with all those pleasures
of exciting spectacle which enter so largely into our enjoyment of
life. It likewise discriminates the forms, sizes, and distances of objects;
but by a process long misunderstood, and dependent upon a set of perceptions
which, although precisely those whence we derive our most fundamental
notions of the objects around us, have been completely overlooked
in that time-honoured enumeration of the senses which recognizes only five.
If such be the extent to which our minds are dependent upon the wonderful
apparatus of the eye, it may easily be imagined what must be the comparative
narrowness of mental development in those who have never enjoyed
this precious sense, and the feeling of deprivation in those, who,
having enjoyed it, have unfortunately lost it. Well may our sublime poet
despairingly ask—
“Since light so necessary is to life,
And almost life itself—if it be true
That light is in the soul—
The all in every part: why was the sight
To such a tender ball as the eye confined,
So obvious and so easy to be quenched?”
—for he himself, in his own person, experienced this deprivation, and he
thus touchingly, in his great work, laments his loss:
“Thus with the year
Seasons return; but not to me returns
Day, or the sweet approach of even or morn,
Or sight of vernal bloom, or summer’s rose,
Or flocks, or herds, or human face divine;
But cloud instead, and ever-during dark
Surround me; from the cheerful ways of men
Cut off; and for the book of knowledge fair
Presented with a universal blank
Of Nature’s works—to me expunged and rased,
And wisdom at one entrance quite shut out.”
An organ which is the instrument of so many nice discriminations as is
the eye must, of course, present the most delicate adjustment in its parts.
So much has in recent times been learnt of the nature of its mechanism;
of the relation between the impressions made upon it and the judgments
formed by the mind therefrom; of the illusions which its very structure
produces; of the defects to which it is liable; and of its wonderfully
454refined physiological elements—that a branch of science sufficiently extensive
to require a large part of a studious lifetime for its complete mastery
has grown up under the hands of modern physiologists, physicists, and
psychologists. To some of the results of their labour we would invite the
reader’s attention; and in order to render the account of them intelligible,
we must, to a certain extent, describe “things new and old.”
Fig. 234.—Vertical Section of the Eye.
The form of the human eye and the general arrangement of its parts may
be understood by referring to Fig. 234, which is a section of the eyeball.
It has a form nearly globular, and is covered on the outside by a tough
firm case, A, named the sclerotic coat, which is, for the most part, white
and opaque. This covering it is which forms what is commonly termed
the “white of the eye;” but in the front part of the eyeball it loses its
455opacity, and merges into a transparent substance, termed the cornea, B.
The cornea has a greater convexity than the rest of the exterior of the eyeball,
so that it causes the front part of the eye to have a somewhat greater
projection than would result from its general globular form. This sclerotic
coat—with its continuation, the cornea—serves to support and protect the
more delicate parts within, and is itself kept in shape by the humours,
which fill the whole of the interior. The greater space is occupied by the
vitreous humour, C; but the space immediately behind the transparent
cornea is filled with the aqueous humour, D. The latter is little else than
pure water, and the former is like thin transparent jelly. The cavities containing
these two humours are separated by the transparent double convex
lens, E, called the crystalline lens, which, in consistence, resembles very
thick jelly or soft gristle. The outward surface of this lens has a flatter
curvature than the inner surface. Immediately in front of the crystalline
lens is found the iris, F, which may be described as a curtain having in the
middle a round hole. The iris is the part which varies in colour from one
individual to another—being blue, brown, grey, &c.; and the aperture in
its centre is the dark circular spot termed the pupil.
The general disposition of the parts of the eye with regard to light will
be most easily understood by comparing it with an optical instrument, to
which it bears no little resemblance, namely, the camera obscura, so well
known in connection with photography. We may picture to ourselves a
still more complete resemblance, by imagining that the lens of the camera
is single, that we have fixed in front of it a watch-glass, with the convex side
outwards, and that we have filled with water the whole of the interior of
the camera, including the space between the watch-glass and the lens. The
focussing-screen of the camera corresponds with the inner surface of the
back of the eyeball, about which we shall presently have more to say. Now,
even if the camera had no lens, but were simply a box filled with water,
and having in front the watch-glass, fixed in the manner just mentioned,
we could obtain the images of objects on the screen, as a consequence of
the curvature of the watch-glass. It would, however, in this case, be necessary
to have the camera much longer, or, in other words, the rays would
be brought to a focus at a greater distance than if we put in the glass lens,
which would, thus placed in the water, cause the rays to converge to a
focus at a much shorter distance, although its effect when surrounded by
water would be less powerful than in the air. There we see the effect of
the crystalline lens of the eye in bringing the rays to a focus within a much
shorter distance than that which would be required had there been present
only the curved cornea, and the aqueous and vitreous humours of the eye,
which are but little different from pure water in their optical properties.
If we focus the camera by adjusting the distance between the lens and
the screen so as to get a distinct image of a near object, we should find, on
directing the instrument to a distant one, that the image would be blurred
and indistinct, and the lens would have to be moved nearer to the screen;
or we could get the image of the distant object distinct by replacing the
lens by another lens in the same position, but having some flatter curvature.
It is plain that the same object would be gained if our lens could be
made of some elastic material, which, on being pulled out radially at its
edges, could be made to assume the required degree of flatness without
losing its lenticular form. Now, it is precisely with an automatic adjustment
of this kind that the crystalline lens of the eye is provided, for the
lens is suspended by an elastic ligament, G, by the tension of which its surfaces
456are more flattened than they would otherwise be; but when the tension
of this ligament is relaxed, by the action of certain delicate muscles
which draw it down, the elasticity of the lens causes it to assume a more
convex form.
Fig. 235.Section of Retina.
These optical adjustments give, on the inner surface of the coats of the
eye, a more or less perfect real image of the objects to which the eye is
directed, and it is on the back part of this inner surface that the network
of nerves, called the retina, H, is spread out. The sclerotic coat, already
spoken of, is lined internally with another, named the choroid, which is
composed of delicate blood-vessels, intermingled
with a tissue of cells filled with
a substance of an intensely black colour.
It is upon this last layer that the delicate
membrane of the retina is spread out between
the choroid and the vitreous humour.
The retina is, in part, an expansion of the
fibres of the optic nerve over the back part
of the eyeball. If we suppose the globe of
this cut vertically into two portions, and so
divide the front from the back part of the
eye, the retina would be seen spread out on
the concave surface of the back part, and in
the middle of this part, opposite the crystalline
lens, would be seen a spot in which
the retina assumes a yellowish colour, and
in the centre of this, a little round pit or
depression. The spot is called the macula
lutea, or yellow spot, and the little central
pit, which is of the highest importance in
vision, is termed the fovea centralis. A
little way from the yellow spot, and nearer
the nose, is a point from which a number
of fibres are seen to radiate, and this is, in
fact, the part at which the optic nerve enters
the eyeball, and from which it sends out its
ramifications over the retina. This part,
for a reason which will shortly appear, is
called the blind spot.
When the minute structure of the retina
is examined by the microscope, its physiological
elements are found to undergo very
remarkable modifications at the yellow
spot. In the retina, although the total
thickness does not exceed the 1 80th part of
an inch, no fewer than eight or ten different
essential or nervous layers have been distinguished. Fig. 235 rudely represents
a section. The lowest stratum, A, which is next the choroid, and forms
about a quarter of the total thickness, is formed of a multitude of little
rod-shaped bodies, a, ranged side by side, and among these are the conical
or bottle-shaped bodies, b. This lowest stratum of the retina is called the
layer of rods and cones. At their front extremities the rods and cones pass
into very delicate fibres, which, going through an extremely fine layer of
fibres, B, are connected with a series of small rounded bodies, which form
457the layer of nuclei, C, separated by a layer of nervous fibres, D, from a
granular layer, E, in front of which is a stratum of still finer granules, F,
underlying a layer of ganglionic nerve-cells, G, of a larger size than any of
the other elements, and these ganglionic cells send out numerous branching
nerve-fibres, forming the layer H. Finally, on the front surface of the retina
there is a thin stratum formed of fibres, which issue from the optic nerve, K,
Fig. 234, and in fact constitute the expansion of this nerve on the inner
surface of the eyeball. The terminations of some, at least, of these nerve-fibres
have been traced, and have been found to form junctions with those
branching from the ganglionic cells.
Fig. 236.
Of the part played by each of these delicate structures in exciting visual
impressions little is yet known. How light, or the pulsations of ether, if
such there be, is ultimately converted into sensation will probably for ever
remain a mystery, although it is quite likely that the kind of visual impression
which is conveyed by each part of the elaborate structure of the retina
may ultimately be distinguished. One curious result of modern investigation
is that light falling directly upon fibres of the optic nerve is quite
incapable of exciting any sensation whatever. Light has no more effect on
this nerve and its fibres than it would have on any other nerve of the body
if exposed to its action. The apparatus of rods, cones, and other structures
are absolutely essential to enable light to give that stimulus to the optic
nerve which, conveyed to the brain, is converted into visual sensations. So
if this apparatus were absent in our organs of vision, in vain would the
optic nerve proper be spread out over the interior of the eyeball: we should
be no more able to see with such eyes than we are able to see with our
hands.
We now invite the reader’s careful consideration to the diagram, Fig. 236,
which is a section of the retina through the yellow spot. The upper part
of the figure is the front, and the deep depression is the little pit already
spoken of—the fovea centralis. The lowest dark line represents the basement
membrane of the retina, and immediately above is seen the layer of
rods and cones, and the various strata already spoken of are represented
in their due order in the marginal parts of the diagram. Now observe the
remarkable modifications of the nervous structures in the neighbourhood
of the fovea centralis, some of which are visible in the diagram. In the
first place, the cones are there much longer, more slender, and more closely
set, so that there is a far greater number of them on a given surface; but
458the rods are comparatively few, and are, in fact, not found at all under the
floor of the little pit. The layer of nuclei, into which the cones extend, is
thinner, and is found almost immediately below the anterior surface, for
all the other layers thin out in the fovea in a very curious manner. It is,
however on the margin of the fovea that the stratum of ganglionic cells, G,
Fig. 235, attains its greatest thickness, for there it is formed by the superposition
of eight or ten cells, being here thicker than any other layer, while
it is so thinned off towards the margin of the retina that it no longer forms
even a continuous stratum. This layer, however, becomes much thinner
in the fovea, which contains, in fact, but few superposed cells. The tint of
the yellow spot is said to be derived from a colouring matter, which affects
all the layers except that of the cones. The centre of the yellow spot,
where the fovea centralis is situated, is extremely transparent, and is so
delicate that it is very easily ruptured, and has frequently been taken for
an aperture.
We should not have risked wearying the reader with these details concerning
the little pit in the centre of the retina had it not possessed an
extreme importance in the mechanism of the eye, a fact which he will at
once appreciate when we say that of the whole surface of the retina, the only
spot where the image of an object can produce distinct vision is the fovea
centralis. Since this is undoubtedly true, it follows that the physiological
elements which we there find are precisely those which are most essential
for producing this effect. The case may be exemplified by recurring to
the comparison of the eye with a photographer’s camera, by supposing his
screen to be of such a nature that only on one very small spot near its
centre could a distinct image be possibly obtained of just one point of an
object. Such a defect in his camera would render the photographer’s art
impossible, and this defect (if it may be so called) in the eye would render
it almost equally useless, had not an adjustment, which more than compensates
for it, been afforded in the extreme mobility of our organs of vision.
This adjustment is so perfect that people in general do not even suspect that
the image of each point of an object which they distinctly see must be formed
on one particular spot on the retina—a spot about one-tenth of the diameter
of an ordinary pin-head! We may venture, without any disrespect to the
reader, to assume that the chances are that it is new to him to learn how each
letter in the lines beneath his eye must successively, but momentarily, form
its image in the very little pit in the centre of his retina; and the chances are
at least a hundred to one that, even if aware of this, he has passively received
the statement, and that he has not made the least attempt to realize the truth
for himself. Yet nothing is easier. Let him request a friend to slowly peruse
some printed page, while he meanwhile intently watches his friend’s eyes.
He will then perceive that before a single word can be read there is a movement
of the eyeballs, which are, quite unconsciously to the person reading,
so directed that the image of each letter (for the area of distinct vision is
incapable of receiving more than this at once) shall fall upon the only parts
of the retinæ from which a distinct impression can be conveyed along the
optic nerve. Thus it is that the eye, without any conscious effort of the
observer, is directed in succession to the various points of an object, and
it is only by an effort of will in fixing the eyes upon one spot that one becomes
aware of the blurred and confused forms of all the rest of the visual
picture. Yet so readily do the eyeballs turn to any part of the indistinct
picture on which the attention is fixed, that it is not improbable a person
unversed in such experiments, wishing to verify our conclusions by looking,
459say, at one spot on the opposite wall, will be very apt, in thinking of the
features of the rest of the picture, to direct his eyes there, and then declare
that he, at least, sees no such vague forms. If such be his experience,
the correction is easy. He has only to ask some one to watch closely his
eyes while he repeats the experiment, and after a few trials he will succeed
in maintaining the requisite immobility of the eyeballs—a condition
upon which the success of many such experiments depends.
Fig. 237.—Muscles of Eyes.
The muscles of the eyeballs viewed from above:—B, the internal rectus; E, the external rectus; S, the superior rectus; T, the superior oblique, passing through a loop of ligament at U, and turning outwards and downwards to its insertion at C. The inferior rectus and the inferior oblique are not visible in the figure: the superior rectus is removed from the right eyeball in order to show the optic nerve N.
This extreme mobility of the eyeballs more than compensates for the
loss of the clear and well-defined picture, for it calls into action one of
the most sensitive of all the impressions of which we are capable, and
one which possesses in so high a degree the power of uniting with our
other sensations, that this sixth sense has been, as already stated, utterly
overlooked, except by the more modern students of the nature of our
sensations. It is usually termed the muscular sense, and to it are due
some of the nicest distinctions of impressions of which we are capable. The
muscles of every part of our frame take their part in producing impressions
in our minds, and those of the eyeballs have a very large share in furnishing
us with ideas of forms and motions. Fig. 237 is a diagram showing
the general arrangement of these muscles; and their anatomical designations,
which need not much concern us at present, are given beneath the
figure. The wonder is, that the sensations arising from the relative conditions
of parts so few, should afford us the immense variety of notions referrible
for their origin to these muscles only. We take one example in
460illustration. Suppose we watch the flight of a bird, at such an elevation
that no part of the landscape comes into the field of view at all; and that,
again, we follow with the eye, under similar circumstances, the path of a
rocket. We can unhesitatingly pronounce the motions unlike, and yet in
each case there was no visual impression present but that of the object
focussed upon the yellow spot. But the movement of the muscles in one
case was different from that in the other. Nay more, we can form such a
judgment of the motion as to pronounce that the object followed such and
such a curve—we may recognize the parabola in one path, and the circle,
perhaps, in the other. And this kind of discrimination arises from the fact,
that when we have, maybe times without number, previously looked at
parabolas and circles, in diagrams perhaps, the muscles of the eyeballs
have performed just the same series of movements, as point after point of
the line was made to form its image on the yellow spot. This is not the
only class of impressions that these muscles are capable of affording; there
is, for example, little doubt that they aid us in estimating distance. But
space will not permit further discussion of this subject.
Although the blurred and indefinite retinal picture may be compensated,
and perhaps more than compensated, by the readiness with which
the eyes move, it is, of course, possible that greater precision and delicacy
of visual impression over the whole surface of the retina might be consistent
with a still greater increase of our powers of perception. There are
instances in which the absence of finish, as it may be termed, in all but one
little spot in the picture, proves a real inconvenience and a sensible deprivation.
Perhaps a friend calls our attention to the fact that a balloon is
sailing through the air, or some fine morning, hearing in the fields the
blithe song of the sky-lark, we look up and vainly try to bring the small
image upon the place of distinct vision. Now, if an image which falls upon
any other part of the retina is perceived, even indistinctly, an instant suffices
to direct the eyes into the exact position requisite for clear vision—an example
of the marvellous precision with which impressions are put in relation
to each other by the unconscious action of the brain. But while an
image on the fovea, only 1 6000th of an inch diameter, produces a distinct
sensation, it is found that if the image falls on the retina at a point some
distance from the yellow spot, the image must be 150 times larger in order
to produce any impression; and it is in consequence of the image of balloon
or bird not having the requisite size to give any impression to the less sensitive
portion of the retina, that we grope blindly, as it were, until by chance
the image falls near the yellow spot, when the tentative motion of the eyeballs
is instantly arrested, and the image fixed. On the other hand, the
field of indistinct vision which the eye takes in is extremely wide, for bright
objects are thus perceived, even when their direction forms an angle laterally
of nearly 90° with the axis of the eye; and, if the object be not only bright,
but in motion, its presence is noticed under such circumstances with still
greater ease. Thus, an observer scanning the heavens would have a perception
of a shooting star anywhere within nearly half the hemisphere. The
range is, however, less than 90° in a vertical direction.
We have said that the fibres of the optic nerve, entering the back part
of the eyeball, at K, Fig. 234, ramify over the anterior surface of the retina
in fibres which form a layer of considerable relative thickness. The light,
therefore, first encounters these nerves, and only after traversing their
transparent substance does it reach the deeper seated layer of rods and
cones, where it excites some action that is capable of stimulating the optic
461nerve. These rods and cones might naturally be supposed to be merely
accessory to the fibres of the optic nerve, had we not the following conclusive
evidence that the cones play a necessary part in the action, and that
it is only through them that light acts upon the optic nerve:
Fig. 238.
1. The cones are more developed and more numerous in the spot where
vision is most distinct.
2. The “blind spot” is full of fibres of
the optic nerve, but is absolutely insensible
to light, and is without rods or cones.
3. We can distinguish an image on the
fovea, having only 1 6000th of an inch diameter;
but on the other parts of the retina
the images must have larger dimensions.
It is found that the size of the smallest
distinguishable images agrees nearly with
the diameters of the cones at the respective
parts.
To some readers the fact will doubtless
be new, that a considerable portion
of the eye is quite insensible to
light, namely, that portion already designated
as the “blind spot.” A simple
experiment, made by help of Fig. 238,
will prove this. Place the book so that
the length of the figure may be parallel
to the line joining the eyes, and let the
right eye be exactly opposite the white
cross, and at a distance from it of about
11 in. If the left eye be now closed, while
with the right the cross is steadily viewed
so that it is always clear and distinct,
the white circle will completely disappear,
and the ground will appear of a uniform
black colour. In order to insure success,
the observer must be careful not to look
at the white circle, but at the cross, and
some persons find this more difficult than
others. The position of the blind spot in
the eye has been already mentioned, and
its significance in showing the insensibility
to light of the fibres of the optic
nerve has been pointed out. In the table
of the dimensions of some parts of the
eye, which, for convenience of reference,
is given together below, it will be seen that
the diameter of the blind spot is considerable
compared with the size of the retina,
its greatest diameter being about 8 100 in.
The length on the retina of the image of a man at a distance of 6 ft. or 7 ft.
is not greater than this, so that in a certain position with regard to the eye
a person would, like the white circle, be quite invisible. In like manner,
by looking steadily in a certain direction with one eye, the image of the
full moon may be made to fall upon the blind spot, and the luminary then
462becomes invisible, and would be so even if its apparent diameter were
eleven times greater; so that if we suppose eleven full moons ranged in a
line, the whole would be quite invisible to a person looking towards a certain
point of the sky at no great angular distance from them.
The following are the dimensions in English inches of some parts of the
eye:
In.
Diameter of the entrance of the optic nerve
0·08
Distance of centre of optic nerve from centre of yellow spot
0·138
Diameter of fovea centralis
0·008
Diameter of the nerve-cells of the retina
0·0005
Diameter of the nuclei
0·00003
Diameter of the rods
0·00004
Diameter of the cones in yellow spot
0·00018
Length of rods
0·0016
Length of cones in yellow spot
0·0008
Thickness of retina at the back of the eye
0·0058
By means of an instrument to be presently described, the ophthalmoscope,
it is possible to view directly the whole surface of the retina, and to observe
the inverted images of the objects there depicted. It is thus observed that
it is only on the parts near the yellow spot that the images are formed with
clear and sharp definition. Away from this the definition is less perfect;
and besides the diminished sensitiveness of the retina, this circumstance
contributes to the vagueness of the visual picture, although the falling off
in clearness of vision at a very little distance from the yellow spot is far
more marked than the loss of definition in the image there formed.
Until within the last few years it has been most confidently asserted by
many authors that the eye, considered as an optical instrument, is absolutely
perfect, and entirely free from certain defects to which artificial instruments
are liable. Thus Dr. W. B. Carpenter states, in his “Animal
Physiology” (1859): “The eye is much more remarkable for its perfection
as an optical instrument than we might be led to suppose from the cursory
view we have hitherto taken of its functions; for, by the peculiarities of its
construction, certain faults and defects are avoided, to which all ordinary
optical instruments are liable.” Among the imperfections which are completely
corrected in the eye, he names “spherical aberration” and “chromatic
aberration”—both of which give rise to certain defects in optical
instruments. But by recent careful investigations it has been conclusively
shown that the eye is not free from chromatic aberration; that it has
defects analogous to spherical aberration; and that there are, besides,
certain optical imperfections in its structure, which are avoided in the
artificial instruments. Professor Helmholtz, one of the most distinguished
of German mathematicians, physicists, and physiologists, whose great work
on “Physiological Optics” is the most complete treatise on the subject
which has ever appeared, is so far from considering the eye as possessed
of all optical perfections that he remarks that, should an optician send him
an instrument having like optical defects, he would feel justified in sending
it back. The defects which may be traced in the eye, considered as an
optical instrument, do not, however, he admits, detract from the excellence
of the eye considered as the organ of vision.
When we find that Sir Isaac Newton pointed out the chromatic aberration
463of the eye two centuries ago—when we find that D’Alembert, in 1767,
proved that the lenses of the eye might have as great a dispersive power
as glass without the want of achromatism necessarily becoming noticeable—when
we find that the celebrated optician Dolland, the inventor of the
achromatic lens, showed that the refractions which take place in the eye
all tend to bring the violet rays towards the axis more than the red—when
we find that Maskelyne the astronomer, Wollaston the physicist, Fraunhofer
the optician, and other scarcely less distinguished men of science,
have made actual measurements of the distances of the foci in the human
eye for the different rays of the spectrum—when we find how these defects
have so long ago been observed, examined, and measured as to their amount—the
persistence with which writer after writer has asserted the achromatism
of the human eye appears so extraordinary, that it can only be accounted
for by the prevalence of the preconceived notion that the eye is absolutely
perfect—a notion not without its reason and grounds, in the fact of the
exquisite adaptation of the organ of sight to the needs of humanity.
Although the want of achromatism in the eye thus escapes ordinary
notice, it is, on the other hand, easy to render it evident by simple experiments.
If, for example, we view from a certain distance the solar spectrum
projected on a white screen, it will be found that, when we see the red end
quite distinctly, the violet end will, at the same time, appear vague and
confused, and vice versâ. The author believes that the following very
simple experiment will at once convince any person that the fact is as
stated. Procure a small piece of blue or violet stained glass, and another
piece of red glass, and, having cut out of an opaque screen a rectangular
opening, say ½ in. long and ¼ in. wide, place the glasses close to it, so that
one-half the opening is covered by the red glass and the other half by the
violet glass, the two being placed so that, on looking through the screen, a
violet square and a red square are visible. The opaque screen may be
made of black paper, cardboard, or tinfoil, and the edges of the opening
must be cut perfectly even. On looking through this arrangement, held at
a distance of about two feet from the eye, both squares may be seen distinctly
by a person of ordinary vision; but, at a distance of five inches from
the eye, he will find it impossible to see the squares otherwise than with
vague and ill-defined edges. This is because the crystalline lens cannot
adapt its curvature so as to bring the rays from the object to a focus on the
retina. Now, by trial, the nearest distance at which each of the coloured
squares becomes visible may be found, and it will be observed, that the
violet square is first sharply defined at a less distance than the red, whereas,
if the eye brought the red and violet rays to a focus at the same point,
the smallest distance of distinct vision would coincide in both cases.
The reader may observe the same fact for himself, in even a still simpler
manner, by turning to Fig. 238, page 461. When the white circle is viewed
by one eye, at a distance of about a foot, and an opaque screen, such as a
coin, is held close to the eye, so that the pupil is half covered by it, the
one side of the white circle will appear bordered by a narrow fringe of blue,
and the other side by a narrow fringe of orange. If the opaque screen be
shifted from one side of the pupil to the other, the colours will change
places, the orange appearing always on the same side of the white circle
as the screen is held before the eye. The same appearances are presented
in a still more marked degree when the full moon is made the subject of
the experiment.
The diagram, Fig. 239, shows the course of the red and violet rays from
464a luminous point, A, the refraction being supposed to take place at B1 B2.
The violet rays after refraction form the cone, B1, E, B2, and E is their
focus; the red rays form the cone, B1, F, B2, and have a focus at F. The position
of the retina would be intermediate between E and F, and is indicated
by C1, C2. It will be noticed that the violet rays cross, and are received on
the retina in the same circle, G G, so that the colours, then blended, would
be separately imperceptible; but the point would produce a diffused circular
image of the blended colours.
In viewing an object—the moon, for example—the accommodation of
the eye is like that indicated in the diagram. The distinct image due to
the red rays would be formed behind the retina, and that due to the violet
rays would be in front of it. In the image on the retina the most intense
rays—such as the orange, yellow, and green—are those which are blended
by the adjustment of the eye, and the red and violet form images more
out of focus (to use a common expression), and a very little larger than the
more intense image. We might expect that a white disc would therefore
appear with a fringe of colour, resulting from a mixture of red and violet;
but the fringe is too narrow, and the colour itself too feeble, to become
perceptible. When, however, the pupil of the eye is half covered, the red
and violet images are displaced in different directions, the position of the
retina being too far forward for the one, and too far back for the other. The
coincidence therefore ceasing, the colours show themselves at the margins
of the image.
Fig. 239.
The non-perception under ordinary circumstances of the chromatic aberration
of the eye is largely due to the greater intensity of the colours which
differ least in their refrangibilities. The clearness of our vision does not,
therefore, practically suffer from this defect of the eye. Professor Helmholtz
constructed lenses which rendered his eyes really achromatic, and
looking through these when the pupil was half covered, no coloured fringes
were seen at the edges of dark or light objects, or when the objects were
looked at with an imperfect accommodation of the eye. He was, however,
unable to detect any increase of clearness or distinctness of vision by the
correction.
The eye is also subject to other aberrations and irregular refractions,
which are special to itself; for example, with moderately illuminated objects
the crystalline lens produces images apparently well defined, and nothing
is visible to suggest the absence of uniformity in its structure. But when
the light is intense, and concentrated in a small object surrounded by a dark
field, the irregular structure of the crystalline lens shows itself in the most
marked manner. Every one must have noticed the appearance presented
by the distant street-lamps on a dark night, and by the stars. The latter
465we know to be for us mere points of light, and their images produced by
perfect lenses would also be mere points; instead of which we see what
seem to be rays issuing from the star, an appearance which has given rise
to the ordinary representation of a star as a figure having several rays.
That no such rays actually do emanate from the real star may be easily
proved: first, by concealing the luminous point from view, by means of a
small object held up as a screen. If the rays had any existence outside of
the eye, they would still be seen; instead of which, the whole of them disappear
when the luminous point, or, in the case of the street-lamp, when
the flame, is covered by the screen. A second proof that the origin of
the phenomenon is in the eye, and not in the object, is afforded by the fact
that if, while attentively observing the rays, we incline the head, the rays
turn with the eyes, so that when the head is resting on the shoulder
the ray which appeared vertical
becomes horizontal. The cause
of these divergences from the
regular image lies in the fact of
the crystalline lens being built
up of fibres which have refractive
powers somewhat different
from that of the intermediate substance.
These fibres are arranged
in layers parallel to the surfaces
of the crystalline lens, and the direction
of the fibres in each layer
is generally from the centre to the
circumference; but towards the
axis they form, by bending, a kind
of six-rayed figure, as shown in
Fig. 240, which represents the
arrangement of the fibres of the
external layers of the lens. In the outermost layers the branches of the
star-shaped figure are subdivided into secondary branches, which give
rise to more complicated figures. When we view by night a very brilliant
but small light, even these subdivisions may be traced in the radiating
figure.
Fig. 240.
The light which enters the eye is partly absorbed by the black pigment
of the choroid, and partly sent back by diffused reflection from the retina
through the crystalline lens and pupil. The image of a luminous body as
depicted on the retina of another person cannot be seen by us under ordinary
circumstances, because, by the principle of reversibility already mentioned
as of universal application in optics, the rays which issue from the retinal
images are refracted on leaving the eye, and follow the same paths by
which they entered it, so that they are sent back to the object. An observer
cannot see the retinal image of a candle in another person’s eye,
unless he allows the rays to enter his own, and this cannot be done directly,
because the head of the observer would be interposed between the candle
and the eye observed, and the light would then be intercepted. By holding
a piece of unsilvered plate glass vertically, we may reflect the light of
a candle into the eye of another person, and then the light thrown out
from the retinal image of the candle will, on again meeting the surface of
the glass, be in part reflected to its source, and in part pass through the
glass, on the other side of which it may be received into the eye of an
466observer. The positions of the observed and observing eye may be described
as exactly opposite to and near each other, while the candle is
placed to one side in the plane separating the two eyes, and the glass is
held so that it forms an angle of 45° with the line joining the pupils. Under
these circumstances the observer may see the light at the back of the eye,
but he will not be able to distinguish anything clearly, because his own eye
cannot accommodate itself so as to bring to a focus the rays coming from
the retina of the other, since these rays are refracted by the media through
which they emerge. But, by means of suitable lenses interposed between
the two eyes, the retina and all its details may be distinctly seen and
examined. Such an arrangement of lenses and a reflecting surface constitute
the instrument called the ophthalmoscope (οφθαλμος, the eye) of which
there are many forms, but all constructed on the principle just indicated.
This principle was first pointed out by Helmholtz, who described the first
ophthalmoscope in 1851.
Fig. 241.—Ruete’s Ophthalmoscope.
Ruete’s ophthalmoscope is represented in Fig. 241. The parts of the instrument
are supported on a stand, C, and about the vertical axis of this the
column, D, and the arms, H and K, can turn freely and independently; E is
a concave metallic mirror, about 3 in. in diameter, and having an aperture in
its centre through which the observer, B, looks. The arm, H, merely carries
a black opaque screen, which serves to shield the eye of B from the light of
the lamp, and to reduce, if required, the amount of light passing through the
aperture in the mirror. The arm, K, which is about a foot in length,
carries two uprights which slide along it, and in each of these slides a rod
bearing a lens, which can thus be adjusted into any required position. The
instrument is used in an apartment where all light but that of the lamp can
be excluded. In the instrument just described an inverted image is obtained,
which is sufficient for ordinary medical purposes, but this construction does
467not allow of the examination of retinal images, which is best performed with
an instrument having a plane mirror.
The appearance presented by the back of the eye when viewed in the
ophthalmoscope is represented in Fig. 242. The retina appears red, except
at the place where the optic nerve enters, which is white. On the reddish
ground the retinal blood-vessels can be distinguished; A, A, A, branches
of the retinal artery, have a brighter red colour, and more strongly reflect
the light than the branches, B, B, B, of the retinal vein. Among these, and
especially towards the margin, are seen, more or less distinctly, the broader
vessels of the choroid. Above the optic nerve and a little to the right may
be observed the fovea centralis.
Fig. 242.
During the last twenty years the ophthalmoscope has been the chief
means of extending the knowledge of oculists regarding the diseased and
healthy conditions of the eye. In this way the substance of the lens and
the state of the humours can be directly seen, the causes of impaired
vision can be discovered, and the nature of many maladies made out with
certainty. This modern invention, by which the interesting spectacle of
the interior of the living eye can be observed, has therefore been far from
proving a barren triumph of science. Many insidious maladies can thus
be detected, and may be successfully treated before the organ has become
hopelessly diseased. In some cases the ophthalmoscope gives the most
certain evidence of the existence of obscure and unsuspected diseases of
other parts of the body.
468
Everybody knows that, however well the flat picture of an object
may imitate the colours and forms of nature, we are never deceived into
supposing that we have the real object before us. There must, therefore, be
something different in the conditions under which we see real objects from
those under which we view their pictures. The most favourable circumstances
for receiving an illusive impression of solidity from a flat picture, is
when we view it from a fixed position and with one eye. This is because
one means by which we unconsciously estimate distances depends upon the
changes in the perspective appearances of objects caused by changes in
our point of view. In many cases these changes in the perspective are the
only means we have of judging of the relative distances of objects. But
there is another circumstance which is still more intimately connected with
our perception of solidity. Each eye receives a slightly different image of
the objects before us (unless these be extremely remote), inasmuch as they
are viewed from a different point. When the objects are very near, the two
retinal images may differ considerably, as the reader may convince himself
by viewing with each eye, alternately, objects immediately before him,
while the other eye is closed, and the head all the while motionless. The
nearer objects will plainly appear to shift their positions as seen against
the back-ground of the more distant objects; and a somewhat more careful
observation will reveal changes of perspective, or apparent form, in
every one of these objects. An extreme case is presented in that of a playing
card, or thin book, held in the plane which divides the eyes. The back
or the face, the one side or the other, will be seen, according as the right
or the left eye is opened. If we close the left eye, the displacement and
change of apparent form produced by a slight movement of the head are
sufficiently obvious; a movement of the head 2½ in. to the left causes a
decided change in the relative positions of adjacent objects. It is plain,
however, that it is precisely from a point 2½ in. to the left that the left eye
views these objects, and hence the perspective appearance seen by the
left eye must have the difference due to this shifting of the point of view.
On the other hand, if one looks at a picture, or flat surface, placed immediately
in front, no change in the relative positions of its parts is discernible
by viewing it with either eye alternately. Not but that there is a difference
in the retinal images in the two cases, but there is an absence of any point
of comparison by which the change may be judged. If we take a photograph
of a statue, it will, when viewed by one or the other eye, present the
difference of the retinal images which is due to a flat surface; the parts of
the photographic image will be of slightly different proportions as seen by
each eye. If, instead of the photograph we have before our eyes a statuette,
each eye will see a quite different view: the right eye will see a portion
which is invisible to the left eye, and vice versâ, and, in fact, we shall see
more than half round the object. Here, then, we have certain differences
of the retinal pictures when solid objects are viewed, and these differences
by innumerable repetitions have, unconsciously to ourselves, become associated
with notions of solidity, of something having length, breadth, and
depth, or thickness. The marvellous delicacy of these perceptions will be
alluded to hereafter.
469Let us suppose that the lenses of two cameras are fixed in the positions
occupied by the two eyes, and that a photograph is taken in each camera,
the subject being, for example, a statuette. It is obvious that the differences
of the two photographs would correspond with the differences of the
two retinal images, and that, if a person could view with the right eye only
the photograph taken in the right-hand camera, and with the left eye the
left-hand photograph only, there would be formed on the retinæ of his eyes
images very nearly corresponding with those which the actual object would
produce, and the result would be, if these retinal pictures occupied the
proper position on the eyes, that the impression of solidity would be produced,
which is called the stereoscopic effect.
This may be done without the aid of any instrument, as almost any person
may discover after some trials with nothing but a stereoscopic slide, if
he can succeed in maintaining the optic axis of his eyes quite parallel. In
such a case he will observe the stereoscopic effect by the fusing together, as
it were, into one sensation, of the impression received by the right eye from
the right photograph, with that received by the left eye from the left photograph.
But as each eye will, at the same time, have the photograph intended
for the other in the field of view, the observer will be conscious of
a non-stereoscopic image on each side of the central stereoscopic one.
These outside images are, however, very distracting, for the moment the
attention is in the least directed to them, the optic axes converge to the
one side or the other, losing their parallelism, and the stereoscopic effect
vanishes, because the images no longer fall in the usual positions on the
retinæ. It is, in consequence, only after some practice that one succeeds
in readily viewing stereoscopic slides in this manner, but the acquirement
is a convenient one when a person has rapidly to inspect a number of such
slides, for he can see them stereoscopically without putting them in the
instrument. Many persons, however, find great difficulty in acquiring this
power. In such cases it is well to begin by separating the two photographs
by means of a piece of cardboard, covered with black paper on both sides.
When this is held in the plane between the eyes, each eye sees only its
own photograph, and the observer is not troubled with the two exterior
images. After a little practice in this way, the cardboard may usually be
dispensed with, and the observer will insensibly have acquired the habit
of viewing the slides stereoscopically, without any aid whatever.
Fig. 243.—Wheatstone’s Reflecting Stereoscope.
Instruments have, however, been contrived which enable one to obtain
the desired result without effort; and one form of these is now tolerably
470well known to everybody. The first stereoscope was the invention of
Wheatstone. The reflecting stereoscope is represented in Fig. 243, and
consists essentially of two plane metallic mirrors inclined to the front of the
instrument at angles of 45°, so that in each of them the observer sees only
the design which belongs to it. The rays reach the eyes as if they came
from images placed in front of the observer; and the two images having
the proper differences, produce together the impression of solid objects.
Fig. 244.
Brewster’s stereoscope—which is far more widely known than Wheatstone’s—has
two acute prisms, or, more usually, two portions of a convex
lens are cut out, and placed with their margins or thin parts inwards, and
they thus produce the same effect as would be obtained by combinations
of a prism with a convex lens. Another very common form of the stereoscope
has merely two convex lenses. The
effect of the convex lenses is to increase the
apparent size of the images by diminishing the
divergence of the rays emitted by each point,
producing the appearance of larger designs
seen at a greater distance. The effect of the
prism is to give the rays the direction which
they would have if they proceeded from an
object placed in a position immediately between
the two designs, and an additional element
by which we estimate distance, namely,
the convergence of the optic axes, is made to
aid in the illusion, when the rays proceeding
from the two different pictures have approximately
the inclination that they would have if
they emanated from real objects at the place
where the image is apparently formed. The
box or case in which the lenses or lenticular
prisms are placed takes various forms. One
of the most common is represented in Fig.
244, but the stand on which it is mounted is not
a necessary part of the instrument, although
it is sometimes convenient. A handsome
form is met with as a square case, enclosing a number of photographic
stereoscopic views mounted on an endless chain in such a manner that
they are brought successively into view by turning a knob on the outside.
When an instrument of this kind is fitted up with a series of the beautiful
landscape transparencies, which are produced by certain continental photographers,
a more perfect reproduction of the impressions derived from
nature, exclusive of colour, cannot be conceived. We seem to be present
on the very spots which are so truthfully depicted by the subtile pencil of
the sunbeam; we feel that we have but to advance a foot in order to mix
with the passengers in the streets of Paris or of Rome, and that a single
step will bring us on the mountain-side, or place us on the slippery
glacier; at our own fireside we can feel the forty centuries looking down
upon us from the heights of those grand Egyptian pyramids, and find ourselves
bodily confronted with the mysterious Sphinx, still asking the solution
of her enigma. The truth and force with which these stereoscopic
photographs reproduce the relief of buildings are such, that when one sees
for the first time the real edifice of which he has once examined the stereoscopic
images, it no longer strikes him as new or unknown; for he derives
471from the actual scene no impression of form that he has not already received
from the image.
Fig. 245.
But of all subjects of stereoscopic photography the glaciers are, perhaps,
those which best show the
power of the instrument as
far surpassing all other resources
of graphic presentation.
The most careful
painting fails to convey
a notion of the strange
glimmer of light which fills
the clefts of the ice, seen
through the transparent
substance itself. The
simple photograph commonly
presents nothing
but a confused mass of
grey patches; but combine
in the stereoscope
two such photographs,
each formed of nothing
but slightly different grey
patches, and a surprising
effect is at once produced:
the masses of ice assume
a palpable form, and the
beautiful effects of light
transmitted or reflected
by the translucent solid
reveal themselves. Another
very beautiful class
of subjects for stereoscopic
slides is found in those
marvellous instantaneous
photographs, which seize
and fix the images of the
waves as they dash upon
the shore. Here a scene
which has tasked the
power of the greatest
painter is brought home
to us with such force and
vividness that we all but
hear the wild uproar of
the breakers.
But for the art of photography
the stereoscope
would not thus be ready
to minister to our enjoyment, for no pictures wrought by man’s handiwork
could approach the requisite accuracy which the two stereoscopic pictures
must possess. All attempts to produce such pictures by engraving or lithography
have failed, except only in the case of linear geometrical designs,
such as representations of crystals. A very useful and suggestive application
472of the stereoscope has been made to the illustration of a treatise on
solid geometry, where the lines representing the planes, being drawn in
proper perspective, the reader by placing a simple stereoscope over the
plates sees the planes stand out in relief before him, and the multitude of
lines, angles, &c., which in a simple drawing might be distracting even for
a practised geometrician, assume a clear and definite form. The difference
between the two retinal pictures of objects is so slight, that when the objects
are at a little distance, ordinary observation fails to discover it without the
aid of special instruments; and an inspection of the pair of photographs in
a stereoscopic slide will convince any one that, even in these, close and
careful observation is required to perceive the difference.
Some of the principles of stereoscopic drawings may be seen exemplified
by the pair we give in Fig. 245. With this figure the reader may attempt
the experiment of seeing the stereoscopic effect without the stereoscope.
When he has succeeded in doing this, or when he fuses the images together
by placing a simple stereoscope over the page, he will find the result very
singular; for he will receive the impression of a solid crystal of some dark
polished substance—black lead, for instance—placed on a surface of the
same material. The edges of the solid will appear to have a certain lustre,
such as one sees on the edges of a real crystal. The reason of this impression
being produced by two drawings, one of which is formed by black
lines on a white ground, while the other has white lines on a black ground,
is probably due to the circumstance that we very often see in nature the
lustrous edges of an object with one eye only. That is, one eye is in the
path of the rays which are regularly reflected from the object, while the
other is not,—a fact which may be verified in an instant by looking first with
one eye and then with the other, at a polished pencil, or similar object,
when placed in a certain position.
There is a kind of modification of the reflecting stereoscope, known under
the name of the pseudoscope, which is highly instructive, as showing how
much our notions of the solidity of objects are due to the differences of
the retinal images. In the pseudoscope the rays reach the eyes after passing
through rectangular prisms in such a manner that objects on the right
appear on the left, and objects on the left appear on the right; but the
images agree by reason of the symmetry of the reflection, although the
image of the objects that without the instrument would be formed in the
right eye is, by the action of the prisms, formed in the left eye, and vice
versâ. The impressions produced are very curious: convex bodies appear
concave—a coin, for example, seems to have the image hollowed out, a
pencil appears a cylindrical cavity, a globe seems a concave hemisphere,
and objects near at hand appear distant, and so on. These illusions are,
however, easily dispelled by any circumstance which brings before the
mind our knowledge of the actual forms, and by a mental effort it is possible
to perceive the actual forms even with the pseudoscope, and indeed
to revert alternately, with the same object, from convexity to concavity.
This last effect is very curious, for the object appears to abruptly change
its form, becoming alternately hollow and projecting, according as the mind
dwells upon the one notion or the other; but the experiment is attended
with a feeling of effort, which is very fatiguing to the eyes.
Professor Helmholtz has contrived another very curious instrument,
depending on the same principles as the stereoscope. He terms it the
telestereoscope, and while the effect of the pseudoscope is to reverse the
relief of objects, the telestereoscope merely exaggerates this relief; hence
473this instrument is well adapted for making those objects which from their
distance present no stereoscopic effect, stand out in relief. The distance
between our eyes is not sufficiently great to give us sensibly different views
of very distant objects, and what the telestereoscope does is virtually to separate
our eyes to a greater distance. Fig. 246 is a horizontal section of the
instrument. L and R represent the position of the eyes of the spectator;
a, b, are two plane mirrors at 45° to his line of sight; A, B, are two larger
plane mirrors, respectively nearly parallel to the former. c d aL and f g bR
show the paths of rays from distant objects, and it is obvious that the right
eye will obtain a view of the objects identical with that which would be
presented to an eye at R´, while the left eye has similarly the picture of the
objects as seen from the point L´. The four mirrors are mounted in a box,
and means are provided for adjusting the positions of the larger mirrors,
as may be required. With this instrument the distant objects in a landscape—a
range of mountains, for example—which present to the naked eye
little or no appearance of relief, have their projections and hollows revealed
in the most curious manner.
Fig. 246.—The Telestereoscope.
It is upon a similar principle that stereoscopic views of some of the
celestial bodies have been obtained. Admirable stereoscopic slides of
the moon have been produced by photographing her at different times,
when the illumination of the surface is the same, but when, in consequence
of her libration, somewhat different views of our satellite are presented
to us. Two such photographs, properly combined in the stereoscope, give
not only the spherical form in full relief, but all the details of the surface:
the mountains, craters, valleys, and plains are seen in their true relative
projection.
The telestereoscope may be inverted, so to speak, and its effect reversed;
for an arrangement of mirrors similarly disposed, but on such a scale as
will permit the eyes to be respectively in the lines c d and f g, would reflect
from objects in the direction L R rays which would have but little of the
difference of direction to which the stereoscopic effect is due. Hence solid
objects viewed with such an instrument appear exactly like flat pictures, the
effect being far more marked than in simply viewing them with one eye.
An ingenious method of exhibiting a stereoscopic effect to an audience
474has been contrived by Rollmann. He draws on a black ground two linear
stereoscopic designs—that for the left eye with red lines, that for the right
eye with blue. Each individual in the audience is provided with a piece
of blue glass and a piece of red: he places the red glass before the left eye,
the blue glass before the right: each eye thus receives only the picture
intended for it, for the blue lines cannot be seen through the red glass, or
the red lines through the blue glass. The diagrams may, of course, be
projected on a screen by a magic lantern, in which case the circumstances
are even more favourable. Duboscq has arranged a kind of opera-glass,
so that a person may view appropriate designs on the large scale, and
arrangements have been also contrived by which the stereoscopic effect
may be seen in moving figures.
Every student of this interesting subject should examine a few stereoscopic
images produced by simple lines representing geometrical figures,
or the photographs of the model of a crystal, as these exhibit in the most
striking manner the conditions requisite for the production of stereoscopic
effects. A person having a little skill in perspective and geometry might
construct the two stereoscopic images of a body defined by straight lines,
but the drawings must be executed with extreme exactitude, for the least
deviation would produce the most marked effect in the stereoscopic appearance.
The production of stereoscopic photographs now forms a considerable
branch of industrial art. At first, these photographs were made by
taking the two different views with the same camera at two operations.
But there were difficulties in obtaining uniformity of depth in the impressions,
and the change in the shadows produced by the earth’s rotation
showed itself—although the interval between the two exposures might not
exceed three or four minutes. The increased shadows in such cases show
themselves in the stereoscope, like dark screens suspended in the air. It
was Sir David Brewster who, in 1849, first proposed the plan now universally
adopted, of producing the views simultaneously by twin cameras forming
their images on different parts of the same sensitive plate, the centres
of the lenses being placed at the same distance apart as a man’s eyes, that
is, from 2½ to 3 in. This is, of course, the only manner in which instantaneous
views can be secured. Helmholtz, however, advocates the photographs
of remote objects being taken at a much greater distance apart, for
they otherwise present little appearance of relief. By selecting from an
assortment of slides, two views of the Wetterhorn, taken from different
points in the Grindelwald valley, and combining these in the stereoscope,
he found that a far more distinct idea of the modelling of the mountain
could be thus obtained than even a spectator of the actual scene would
receive by viewing the mountain from any one point. Such a mode of combining
the photographs would produce in the stereoscope the same effect as
the telestereoscope would in the landscape, but the effect would be caused
to a proportionately far higher degree.
The date of Wheatstone’s first publication regarding the stereoscope was
1833; but a complete description and theory of the instrument was not
published until five years afterwards. Brewster first made public, in 1843,
his invention of the stereoscope with lenses, which is now so familiar to us,
and few scientific instruments have become so quickly and extensively
popular; certainly no other simple and inexpensive instrument has contributed
so largely to the amusement and instruction of our domestic circles.
And, to the philosopher who studies the nature of our perceptions, the
stereoscope has been even more instructive, for, instead of vague surmises,
475it provided him with the solid ground of experiment on which to found his
theories. The literature of this one subject—stereoscopic effect—is extensive
enough to occupy a tolerably long book-shelf. It dates from 300 B.C.,
when Euclid touched upon the subject in his Optics; and after a lapse of
more than eighteen centuries it was taken up by Baptista Porta, in 1583;
but the whole development of this subject belongs almost entirely to the
last half-century.
Fig. 247.
The part which the muscles of the eyes take in our perceptions of form
has been already alluded to, and it may be interesting to illustrate this
point by a curious example or two of illusions arising from their movements.
If our reader will glance at Fig. 247, he will see that the lines, a b
and c d, appear to be farther apart towards the centre than at the ends,
while f g and h i, on the other hand, appear nearest together in the middle.
He will hardly be convinced that in each case the lines are quite parallel
until he has actually measured the distances. A still more striking example
of the same kind of illusion is shown by Fig. 248, due to Zöllner. This
appears a sort of pattern, in which the broad bands are not upright, but
sloping alternately to the right and left, and with the spaces between the
lines wider at one end than the other. The lines in the figure are, however,
strictly parallel. The illusion by which they appear divergent and
convergent is still more strongly felt when the book is held so that the
wider bands are inclined at an angle of 45° to the horizon. There is another
illusion here with reference to the short lines, which will appear to be opposite
to the white spaces on the other side of the long lines to which they are
attached. That these illusions are really due to movements of the eyes
may be proved by viewing the designs in any manner which entirely prevents
the movement, as by fixing the gaze on one spot in the case of
Fig. 247, when the illusion will vanish; but this plan is not so easily applied
to Fig. 248. A convincing proof, however, will be found in the appearance
of these figures when they are viewed by the instantaneous light of the
electric spark, as when a Leyden jar is discharged in a dark room. The
reader viewing the figures, held near the place where the spark appears,
476will see them distinctly without the illusions as to the non-parallelism of the
lines. In the absence of an electrical machine, or coil and jar, the reader
may have an opportunity of seeing the figures by flashes of lightning at
night, when the result will be the same.
Fig. 248.
There is a property of the eye which
has led to the production of many amusing
and curious illusions. This property
in itself is no new discovery, for its presence
and effects must have been noticed
ages ago. The property in question is
illustrated when we twirl round a stick
or cord, burning with a red glow at the
end. We seem to trace a circle of fire;
but as the glowing spark cannot be in
more than one point of the circle at once,
it is plain that the impression produced
on the eye must remain until the spark
has completed its journey round the
circle, and reaching each point successively
renews the luminous impression.
Like other subjects relating to vision,
this phenomenon has been carefully examined
in recent times, and its laws
accurately determined.
The fact which is obvious from such an experiment, may be thus stated:
Visual impressions repeated with sufficient rapidity produce the effect of
objects continually present. This persistence of the visual impressions is
easily made the subject of experiment by means of rapidly rotating discs;
and in the common toy called a “colour top” we have a ready means of
verifying some of the conclusions of science on this subject. Some very
interesting results may be obtained by an apparatus as simple as this, regarding
the laws of the phenomenon we are considering, and the effects of
various mixtures of tints and colours.
The well-known toy, the thaumatrope,
depends on the same principle. In this
a piece of cardboard is painted on one
side, with a bird, for example, and on
the other side with a cage: when the
cardboard is twirled round very rapidly
by means of a cord fixed at opposite
points of its length, both bird and cage
become visible at once, and the bird
appears in the cage.
Fig. 249.
Fig. 250.
Fig. 251.
A still more ingenious application of
this principle we owe to Plateau, who
described it in 1833, under the title of
the phenakistiscope; and also to Stampfer,
who independently devised the same
arrangement about the same time, and
named it the stroboscopic disc. The
reader may, at almost any toy-shop, purchase one of them, provided with
a number of amusing figures; or he may easily construct for himself one
which will exemplify the principle. He requires no other materials than
477a piece of cardboard, and his only tools may be a sharp penknife, a pair
of compasses, and a flat ruler. Let him draw on his cardboard a circle of
8 in. diameter, and divide its circumference by eight equidistant points.
From these radii should be drawn with the point of the compasses, and
equal distances from the centre marked off upon them, to fix the centres of
the small circles, which must all have exactly the same size (say, 1 in. in
diameter) and be marked by a distinct line. In these are to be marked the
hand of a clock-face in the positions shown in
Fig. 249; and finally, in the direction of the
radii, narrow slips are to be cut out of the
cardboard as shown. If a pin be put through
the centre of the disc, attaching it thus to the
flat end of a cork, so that it can freely rotate
in its own plane, and the disc be turned rapidly
round, as in Fig. 250, in front of a looking-glass,
while the spectator looks through the
slits, he will see the hand on the little dial apparently
turning round, with rather a jerky
movement it is true, somewhat like the dead-beat
seconds-hand that is sometimes seen on
clocks. The illusion is best when the slits are
so narrow that only one of the several images
is visible by reflection, namely, that which is
adjacent to the slit. Thus, as the disc rotates,
each little circle is visible for an instant as the slit passes in front of the
spectator’s eye; and if the rotation be sufficiently rapid, the impression of
the disc is permanent, as it is constantly being renewed by the successive
circles, while, on the contrary, the hands, having different positions, produce
images in different positions, giving the appearance of a jerky rotation.
The instruments sold in the shops have sometimes a thin metallic disc
with the slits in it, and a series of designs printed in smaller paper discs.
The paper discs may be screwed on the other disc as required, and a
button on a pulley with an endless band is provided for producing the
478rotation more conveniently. Fig. 251 shows one of the pictures for a disc
with twelve slits, and the effect produced by it is that of a dancing figure.
Another arrangement for showing the same illusion has lately become a
very popular toy, and quite deservedly so, for it has the advantages of requiring
no looking-glass, and of making the effect visible to a number of
persons at the same time. This apparatus, which has been termed the
Zoetrope, consists simply of a cylindrical box, like a drum with the upper end
cut off. It is mounted on a pivot, which permits its revolving rapidly about
its vertical axis when touched by the finger. The cylinder has a number of
equidistant vertical slits round the upper part of its circumference. The
figures which produce the illusion are printed on a slip of paper, which is
placed in the lower part of the drum, and when this is in rapid rotation,
and the figures are viewed through the slits, the illusion is produced in
exactly the same manner as in the revolving disc.
Fig. 251a.—Edison’s Kinetographic Theatre.
At the end of the article on the phonograph in a subsequent page, the
reader will find a remark as to the effect that might be produced by a
combination of that instrument with instantaneous and simultaneous
photographs of some famous speaker. This combination has now been
accomplished by the great inventive genius to whom we are indebted for
the phonograph. Mr. Edison has done this so effectively that he may be
said to have given life to the zoetrope by the perfection in which the
ocular illusion is produced together with the audible manifestations that
keep time with it. The amount of thought and ingenuity expended on
this new contrivance, which Edison has called the kinetoscope, will
scarcely be appreciated by anyone who has not given some consideration
to the many practical difficulties that have been overcome. No wonder
that the announcement made at the beginning of 1892 should have been
received with incredulity, for it was to the effect that Edison had contrived
some happy combination of photography and electricity by which
a man (presumably one who could afford to pay for luxuries) might sit in
his own room and see the moving forms of the actors in an opera projected
on a screen before his eyes, while at the same time he would hear their
voices singing. Every movement, every change of expression, every
glance of the eye, and, in fact, all that was visible to the spectator in front
of the stage would appear on the screen, while not a note of vocalist, or
chord of orchestra, would fail to reach the ear. And all this was to be
evoked at will, and repeated as often as desired, not, therefore, of course,
as a presentation of what was taking place at the time, but as a reproduction
of some previous performance. This wonderful result has
virtually been attained by the application of delicate and ingenious
machinery designed to make the phonograph and the camera work
synchronously. The first part of the problem was the production of a
succession of so-called instantaneous photographs at an extremely rapid
rate. In the actual apparatus forty-six photographs are taken every
second, a feat which would beforehand be thought impracticable. This
is accomplished by making use of a band of sensitive celluloid film,
which alone admits of being moved and stopped with the desired rapidity.
The movement is imparted by an electric motor, and the arrangement is
such that for each exposure the film is held stationary for 9 10ths of 1 46th
of a second, during which the lens is uncovered, then for the remaining
⅒th it is covered, while at the same time the film is jerked forward so as
to expose a fresh surface to receive a new impression. Obviously the
mass moved and stopped with this rapidity (which without the stoppages
480is at the rate of 26 miles an hour) must be small, and it is found that
photographs about 1 in. in diameter cannot be much exceeded in view
of this condition. The lens has to be entirely stopped or screened
during the tenth of the short interval (1 460th of a second) in which the onward
movement of the film is taking place, and it has to be practically
open during the remaining 9 10ths of the interval (9 460ths of one second)
in which the film is held stationary in order to receive the photographic
image. These alternations of movement and stoppage must take place
with the utmost regularity, and Edison has used a beautifully regulated
electro-motor as the active power, which also simultaneously moves a
phonograph so that sights and sounds shall proceed in step, for it is thus
they have to be reproduced. This is done by developing the band of
film, and from it printing photographic positives on a similar band, whose
images are successively projected on a screen by means of a lantern with
a step by step movement, exactly the same as that by which the original
photographs are taken, while the phonographic cylinder is so timed as to
give off to a loud-speaking instrument the sounds that accompanied the
photographs. A description of the ingenious mechanism by which all
this is accomplished is not suitable for these pages, for it is the result,
rather than the details of apparatuses, that interest the general reader.
In a simpler form of kinetoscope the positive images on the band of film
are viewed directly by single observers, each looking through magnifying
glasses; in this a disc with 46 slits revolves, and in its passage, as each
slit momentarily permits a view of the image, an electric flash simultaneously
lights it up. The same principle is, of course, used in the screen
projections. From the very great number of impressions made on the
eye in one second, there is none of that jerky movement that is observable
in the older appliances. Mr. Edison has found it necessary to
provide a special stage, or rather small theatre, in which the actors of the
little dramas may be photographed with every advantage in the way of
lighting, &c. Fig. 251a shows this kinetographic theatre with the electric
camera in action. The subjects reproducible in the kinetoscope include
the most rapid movements, such as quick dances, blacksmiths hammering
on an anvil, &c., or incidents of ordinary life involving much gesture and
change of facial expression, and nothing can be more amusing than to
see all these shown to the life by the images on the screen, or by the
pictures viewed through the lens, especially if at the same time the
phonograph is made to emit the corresponding sounds.
ELECTRICITY. — ELEMENTARY PHENOMENA OF MAGNETISM AND ELECTRICITY. — THEORY OF ELECTRICITY. — ELECTRIC INDUCTION. — DYNAMICAL ELECTRICITY. — INDUCED CURRENTS. — MAGNETO-ELECTRICITY. — THE GRAMME MAGNETO-ELECTRIC MACHINE. — ELECTRIC LIGHTING AND ELECTRIC POWER. — THE NEW ELECTRICITY.
About sixty years ago a popular book was published having for its
theme the advantages which would flow from the general diffusion
of scientific knowledge. Great prominence was, of course, given to the
utility of science in its direct application to useful arts, and many scientific
inventions conducing to the general well-being of society were duly enumerated.
Under the head of electricity, however, the writer of that book mentioned
but few cases in which this mysterious agent aided in the accomplishment
of any useful end. The meagre list he gives of the instances in
which he says “even electricity and galvanism might be rendered subservient
to the operations of art,” comprises only orreries and models of cornmills
and pumps turned by electricity, the designed splitting of a stone by
lightning, and the suggestion of Davy that the upper sheathing of ships
should be fastened with copper instead of iron nails, with a hint that the
same principle might be extended in its application. At the present day
the applications of electricity are so numerous and important, that even a
brief account of them would more than fill the present volume. Electricity
is the moving power of the most remarkable and distinguishing invention
of the age—the telegraph; it is the energy employed for ingeniously measuring
small intervals of time in chronoscopes, for controlling time-pieces,
482and for firing mines and torpedoes; it is the handmaid of art in electro-plating
and in the reproduction of engraved plates, blocks, letterpress, and
metal work; it is the familiar spirit invoked by the chemist to effect marvellous
transformations, combinations, and decompositions; it is a therapeutic
agent of the greatest value in the hands of the skilful physician.
Such an extension of the practical applications of electricity as we have
indicated implies a corresponding development of the science itself; and,
indeed, the history of electricity during the present century is a continuous
record of brilliant discoveries made by men of rare and commanding genius—such
as Davy, Ampère, and Faraday. To give a complete account of
these discoveries would be to write a treatise on the science; and although
the subject is extremely attractive, we must pass over many discoveries
which have a high scientific interest, and present to the reader so much of
this recently developed science as will enable him to comprehend the
principles of a few of its more striking applications.
The science of electricity presents some features which mark it with
special characters as distinguished from other branches of knowledge. In
mechanics and pneumatics and acoustics we have little difficulty in picturing
in our minds the nature of the actions which are concerned in the
phenomena. We can also extend ideas derived from ordinary experience
to embrace the more recondite operations to which heat and light may be
due, and, by conceptions of vibrating particles and undulatory ether, obtain
a mental grasp of these subtile agents. But with regard to electricity no
such conceptions have yet been framed—no hypothesis has yet been advanced
which satisfactorily explains the inner nature of electrical action,
or gives us a mental picture of any pulsations, rotations, or other motions
of particles, material or ethereal, that may represent all the phenomena.
Incapable as we are of framing a distinct conception of the real nature of
electricity, there are few natural agents with whose ways we are so well
acquainted as electricity. The laws of its action are as well known as
those of gravitation, and they are far better known than those which govern
chemical phenomena or the still more complex processes of organic life.
Definite as are the laws of electricity, there is no branch of natural or
physical science on which the ideas of people in general are so vague.
Spectators of the effects of this wonderful energy—as seen violently and
destructively in the thunderstorm, and silently and harmlessly in the Aurora—knowing
vaguely something of its powers in traversing the densest materials,
in giving convulsive shocks, and in affecting substances of all kinds—the
multitude regard electricity with a certain awe, and are always ready
to attribute to its agency any effect which appears mysterious or inexplicable.
The popular ignorance on this subject is largely taken advantage
of by impostors and charlatans of every kind. Electric and magnetic
nostrums of every form, electric elixirs, galvanic hair-washes, magnetized
flannels, polarized tooth-brushes, and voltaic nightcaps appear to find a
ready sale, which speaks unmistakably of the less than half-knowledge
which is possessed by the public concerning even the elements of electrical
science.
Electricity has also a special position with regard to its intimate connection
with almost every other form of natural energy. Evolved by mechanical
actions, by heat, by movements of magnets, and by chemical actions, it
is capable in its turn of reproducing any of these. It plays an important,
but as yet an undefined, part in the physiological actions constantly going
on in the organized body, and is, in fact, all-pervading in its influence over
483all matter, organic and inorganic—a secret power strangely but universally
concerned in all the operations of nature. We are compelled to regard
electricity not as a kind of force acting upon otherwise inert matter, but
rather as an affection or condition of which every kind of matter is capable,
although we are still unable to form a conjecture of the precise nature of
the action.
We have now to address ourselves to the task of unfolding so much of
the science as will enable the reader to understand the leading principles
of such important applications as electro-plating, illumination, and the
telegraph; and this will necessarily include an account of the grand discovery
of the identity, or at least intimate connection, of magnetism and
electricity.
The distinctive property of a magnet is, as everybody knows, to attract
pieces of iron, and this property having been observed by the ancients
in a certain ore of iron which was found near the city of Magnesia, in Asia
Minor, the property itself came to be called Magnetism. A bar of steel, if
rubbed with the natural magnet or loadstone, acquires the same property,
and if the bar be suspended horizontally or poised on a pivot, it will settle
only in one definite direction, which in this country is nearly north and
south. If a narrow magnetized bar be plunged into iron filings, it will be
found that these are attracted chiefly by the ends of the bar, and not at all
by the centre. It appears as if the magnetic power were concentrated in
the extremities of the bar, and these are termed its poles, the pole at the
end of the bar which points to the north is called the north pole of the
magnet, and the other is named the south pole. If a north pole of one
magnet be presented to the north pole of another, they will repel each other,
and the same repulsion will take place between the south poles, whereas
the north pole of one magnet attracts the south pole of another. In other
words, poles of the same name repel each other, but poles of opposite names
attract each other, or still more concisely, like poles repel, unlike poles
attract each other.
Magnetism acts through intervening non-magnetic matter with undiminished
energy. Thus, the attractions and repulsions of magnetic poles
manifest themselves just as strongly when the poles are separated by a
stratum of wood or stone as when merely air intervenes, and the attraction
of small pieces of iron by a magnet takes place through the interposed
palm of one’s hand without diminution. A delicately suspended needle in
even a remote apartment of a large building moves whenever a cart passes
in the street. It is almost too well known to require mention here, that
iron and steel are the only common substances which are capable of plainly
exhibiting magnetic forces, and, indeed, there are no known substances
capable of so powerful a magnetization as these. But the difference in the
magnetic behaviour of iron and steel is not so well understood, and it is a
point of importance for our subject, and connected with a fundamental law
which governs all magnetic manifestations. A piece of pure iron is very
readily cut with a file, whereas a piece of steel may be so hard that the file
484makes no impression upon it whatever; and hence a piece of pure iron, or
rather iron holding no carbon in combination, and possessed of no steely
quality, is often spoken of as soft iron. When a piece of soft iron is placed
near the pole of a magnet, the iron becomes, for the time, a magnet. If iron
filings be sprinkled over it, they will arrange themselves about the parts of
the iron respectively nearest and farthest from the magnet, thus showing
that the piece of soft iron has acquired magnetic poles. It will be found
on examining these poles that the one nearest the magnet is of the contrary
name to the pole of the magnet, and the farthest is of the same name. The
conversion of the soft iron into a magnet by the influence of a magnetic
pole is termed induction. It need hardly be said that the inductive effect
is more powerful in proportion to the shortness of the distance separating
the piece of soft iron from the magnetic pole, and, of course, the effect is
at its maximum when there is actual contact. Induction thus explains, by
aid of the law of the poles, the attraction which a magnet exercises over
pieces of iron, for it is plain that the inductive influence is accompanied
by attraction between the two contiguous oppositely-named poles of the
magnet, and of the piece of iron. But attraction is not the only force, for
the pole developed at the farthest portion of the piece of iron being of the
same name as the inducing pole, these will be mutually repulsive. The
attractive force will, however, be more powerful on account of the shorter
distance at which it is exerted, and will predominate over the repulsive
force, particularly at short distances, because then the difference will be
relatively greater. At distances from the inducing pole relatively great to
the distance between the two poles of the piece of iron, the difference may
be so small that its effect in attracting the piece of soft iron will be imperceptible,
and then the piece of iron acted on by two (nearly) equal parallel
forces, will be subject to what is termed in mechanics a couple, the only
effect of which is to turn the body into such a position that the opposing
forces act along the same line. The definite direction assumed by a freely
suspended needle may be explained by supposing that the earth itself is a
magnet having a south pole in the northern hemisphere, and a north pole
in the southern hemisphere, the line joining these poles being shorter than
the axis of the earth, and not quite coinciding with it in position; and the
fact of the needle being turned round but not bodily attracted is then easily
accounted for, the attractive and repulsive forces being reduced to a couple
in the manner just explained.
If the attempt be made to turn a piece of steel into a magnet, by the
induction of a magnetic pole, the same results will be obtained as in the
case of soft iron, but in a much feebler degree, and with this difference:
the piece of steel does not lose its magnetism when the inducing magnet
is withdrawn, whereas in the case of the soft iron every trace of magnetism
vanishes the instant the inducing pole is removed. And if the
pole of the magnet be not only put in contact with one end of the piece of
steel, but rubbed on it, the piece will acquire permanent and powerful
magnetism. Hence it will be noticed that a piece of soft iron can by the
mere approximation of a magnetic pole be converted in an instant into a
magnet, and by the removal of the magnet can as instantly be deprived of
its magnetism, and made to revert into its ordinary condition; while steel
is not so readily magnetized, but retains its magnetism permanently.
Fig. 253.—A simple Electroscope.
The elementary phenomena of electricity are extremely simple and easy
of demonstration, and as the whole science rests upon inferences derived
from these, the reader would do well to perform the following simple experiments
485for himself. Apparatus is represented in Fig. 253, but the only
essential portion is a straw, B, suspended from any convenient support by
a very fine filament of white silk. To one or both ends of the straw a little
disc of gilt paper, or a small ball of elder-pith or of cork, should be attached,
so that the straw may be balanced horizontally. Now rub on a piece of
woollen cloth a bit of sealing-wax, or a stick of sulphur, or a piece of amber,
or a penholder, paper-knife, or comb made of ebonite, and immediately
present the substance to the ball at the end of the straw. It will be first
attracted to the rubbed surface, but after coming into contact with it, repulsion
will be manifested and the ball will separate,
and may be chased round the circle
by following it with the excited body. The
attraction of light bodies by amber after it
has been rubbed appears to be the one solitary
electrical observation recorded by the
ancients, but it has given its name to the
science, ελεκτρον being the Greek name for
amber. The cause, then, of this property
is named electricity, and bodies which exhibit
it are said to be electrified. The reader
will remark that these words explain nothing:
they are used merely to express a
certain state of matter and the entirely unknown
cause of that state. Let the pith
or cork ball at the end of the straw be again
charged with electricity, by bringing it into
contact with a piece of sealing-wax or ebonite
which has just been electrified by friction.
In this condition it will, as we have
just seen, be repelled by the substance which
charged it, and on trial it will be found to be
repelled also by all the substances we have
named, after they have been excited by friction.
But if, while still charged with the
electricity communicated to it by contact
with sealing-wax, sulphur, ebonite, or amber, we present to it a warm and
dry glass tube which has just been rubbed with dry silk, we shall find that
the ball will be strongly attracted. After contact with the glass, repulsion
will take place, and the ball will refuse again to come into contact with the
excited glass. In this condition, however, it will be immediately attracted
by rubbed sealing-wax or ebonite, and so on alternately: the ball when
repelled by the wax is attracted by the glass, and when repelled by the
glass is attracted by the wax.
These simple experiments prove that, whatever electricity may be, there
are two kinds of it, or, at least, it manifests two opposite sets of forces.
The electricity evolved by the friction of glass with silk was formerly called
vitreous electricity, and that shown by excited resin, sealing-wax, amber,
&c., was named resinous electricity. These names have now been respectively
replaced by the terms positive and negative. It must be understood
that these terms imply no actual excess or defect, but are purely distinguishing
terms, just as we speak of the up and down line of a railway, without
implying an inclination in one direction or the other. A fact of great
importance in electrical theory is discovered when the substances in which
486electricity is developed are carefully examined: it is found that one kind
is never produced without the other simultaneously appearing. Thus, the
silk which has been used for rubbing the glass in the above experiments
will be found to exhibit the same electricity as sealing-wax or ebonite.
And, further, the quantities of positive and negative electricity evolved are
always found to be equal, or equivalent to each other; that is, if they are
put together they completely neutralize or destroy each other’s effects. We
have used the word “quantity,” implying that electricity can be measured.
No doubt, whatever electricity may be, there may be more or less of it; but
can we measure an imponderable, invisible, impalpable thing, incapable of
isolation? What we really measure when we say that we measure electricity
is the attractive or repulsive force: we balance this against some
other force (that of gravitation, for example), and we say, so much weight
lifted represents so much electricity.
If we try to electrify a piece of metal by holding it in the hand and rubbing
it against woollen cloth, silk, or other substance, we shall fail in the
attempt: no signs of electricity will thus be shown by the metal. Hence
bodies were formerly divided into two classes—those which could be electrified
by friction, and those which could not. It was afterwards found,
however, that there was no real ground for this division, but that, on the
contrary, no two bodies can be rubbed together, even if they are made of the
same substances, without positive electricity appearing in one, and an equivalent
quantity of negative electricity in the other. The real difference between
bodies which prevents the manifestation of electricity in many cases
depends upon the fact that electricity is able to traverse some substances
with great facility, while others prevent its passage. Thus, if we suspend
horizontally a hempen cord by white silk attached to the ceiling, so that
the hempen cord comes in contact with nothing but the silk, we shall find,
on presenting a piece of excited ebonite to one end of the cord, that electric
attraction of light bodies will be manifested at the other. If a silk cord be
substituted for the hempen one, no such effect will be observed. The hemp
is, therefore, said to be a conductor, and the silk a non-conductor. Again,
if we substitute for one of the silk threads suspending the cord a piece of
twine, or a wire, we shall fail to obtain any electric manifestations at the
remote end, because the electricity will be carried off into the earth by the
conducting powers of these substances. On the other hand, filaments of
glass or ebonite may be used, instead of the silk, with the same effect: they
do not allow the electricity to run through them to the ground, and are
therefore termed, like the silk, insulators of electricity. The distinction of
bodies into conductors on the one hand, and into non-conductors or insulators
on the other, is of paramount importance in the science and in all
its applications. This distinction, however, is not an absolute one: there
is no substance so perfect an insulator that it will not permit any electricity
to pass, and there is no conductor so perfect that it does not offer resistance
to the passage. Substances may be arranged in a list which presents a
gradation from the best conductor to the best insulator. The metals are
by far the best conductors, but there is great relative diversity in their conductive
power. Silver, copper, and gold are much the best conductors
among the metals, iron offering eight times, and quicksilver fifty times, the
resistance of silver. Coke, charcoal, aqueous solutions, water, vegetables,
animals, and steam are all more or less conductors, while among the substances
called insulators may be named, in order of increasing insulating
power, india-rubber, porcelain, leather, paper, wool, silk, mica, glass, wax,
487sulphur, resins, amber, gum-lac, gutta-percha, and ebonite. It will now be
obvious why the electricity developed by the friction of a piece of metal
fails to manifest itself under ordinary circumstances, as, for instance, when
held in the hand: the metal and the body being both conductors, the electricity
escapes. But if the piece of metal be held by an insulating handle
of glass or ebonite, the electrified condition may easily be observed.
The few elementary facts which have been pointed out are absolutely
necessary for the foundation of what is sometimes termed the theory
of electricity, but which is properly no theory,—at least, not a theory in the
same sense as gravitation is a theory explaining the motions of the planets,
or even in the sense in which the hypothesis of the ether and its movements
explains the phenomena of light. It is absolutely necessary to have a conception
of some kind which may serve to connect in our minds the various
phenomena of electricity, if it were only to enable us the more easily to talk
about them. In default of any supposition which will shadow forth what
actually occurs in these phenomena, we have recourse to what has been
aptly termed a representative fiction: we picture to ourselves the actions
as due to imaginary fluids—fluids which we know do not exist, but are as
much creations of the mind as Macbeth’s air-drawn dagger; not, however,
like his “false creation,” proceeding from “the heat-oppressed brain,” but
intellectual fictions, consciously and designedly adopted for the purpose of
enabling us the better to think of the facts, to readily co-ordinate them,
and to express them in simple and convenient language. Non-scientific
persons hearing this language usually mistake its purport, and imagine that
the actual existence of an “electric fluid” is acknowledged. The accounts
which appear in the newspapers of the damage done by thunderstorms
are often amusing from the objectivity which the reporter attributes to the
“electric fluid.” It is described, perhaps, as “entering the building,”
“passing down the chimney,” then “proceeding across the floor,” “rushing
down the gas-pipes,” “forcing its way through a crevice, and then streaming
down the wall,” &c., in terms which imply the utmost confidence of
belief in the existence of the “fluid.” With this intimation that the hypothesis
of electric fluids is merely, then, a “façon de parler,” the reader will
not be misled by the following brief explanation of the elementary facts in
the language of the theory.
In the natural state all bodies contain an indefinite quantity of an imponderable
subtile matter, which may be called “neutral electric fluid.”
This fluid is formed by a combination of two different kinds of particles,
positive and negative, which are present in equal quantities in bodies not
electrified; but when there is in any body an excess of one kind of particles,
that body is charged accordingly with positive or negative electricity. Both
fluids traverse with the greatest rapidity certain substances termed conductors;
but they are retained amongst the molecules of insulating substances,
which prevent their movement from point to point. When one body
is rubbed against another, the neutral electric fluid is decomposed—the
positive particles go to one body, the negative with which these positive
488particles were before united pass to the other body. The particles of the
same name repel each other, but particles of opposite names attract each
other; and it is this attraction which is overcome when the electricities
are separated by friction or in any other manner.
It will be observed that the above is nothing but the statement of the
elementary facts in the language of the hypothesis. This system of the
two fluids readily lends itself to the explanation of nearly all the phenomena
presented in what is termed static electricity—that is, in those phenomena
where the actions are conceivably due to a more or less permanent
separation of the fluids. The grand discoveries in electricity turn, however,
upon quite another condition, namely, one in which the two hypothetical
fluids must be imagined as constantly combining, and here the utility
of the hypothesis is less marked. Inasmuch, however, as there can be no
doubt regarding the identity of the agent operating in the two sets of circumstances,
the facts of dynamical electricity must still be expressed in the
same language, with the aid of any additional conceptions which may give
us more grasp of the subject.
In all electrical phenomena an inductive action occurs, which resembles
that which we have already indicated with regard to magnetism. Thus,
if we take an insulated metallic conductor in the uncharged state, and bring
it near an electrified body, we shall find that the conductor, while still at a
considerable distance, will give signs of an electrical charge. Suppose
we have a cylindrical conductor, and that we present one end of it to the
electrified body, but at such a distance that no spark shall pass, we shall
find, if the charge on the electrified body be strong and the conductor be
brought sufficiently near, that on bringing the finger near the insulated
cylinder, a spark passes. While the cylinder continues in the same position
with regard to the electrified body, no further sparks can be drawn from
it; but if the distance between the two bodies be increased, the insulated
cylinder will be found to have another charge of electricity, which will again
produce a spark. And by repeating these movements we may obtain as
many sparks as we desire by these mechanical actions, without in the
least drawing upon the charge on the original electrified body. The electrophorus
is a device for obtaining electricity by this plan, and several
rotatory electrical machines have lately been invented which yield large
supplies of electricity by a similar inductive action.
Fig. 254.
The Gold-leaf Electroscope.
It is found that in such a case as that we have above supposed, if the
electrified body is charged with positive electricity, the uncharged conductor
brought near it has its electricities separated—the negative attracted and
held by the attraction of the positive charge in the parts of the cylinder
nearest the inducing body; while the corresponding quantity of positive
electricity is driven towards the most remote parts of the insulated conductor.
It is this last which gives the spark in the first case, and if it be not thus
withdrawn from the conductor, it re-combines with the negative electricity
when the conductor is withdrawn from the neighbourhood of the electrified
body, and the conductor then reverts to the natural or unelectrified state.
489But the contact of a conducting body with the conductor while it is under
the influence of the electrified body withdraws only positive electricity, the
negative—being held, as it were, by the attraction of the positive electricity
of the charged body—is not thus removed, and in this condition it is sometimes
called disguised or dissimulated electricity—a term the propriety of
which is doubtful. The excess of negative “fluid” which the conductor
thus acquires shows itself, however, only when the inducing body has been
withdrawn. Precisely similar effects will take place, mutatis mutandis, if
the electrified body has a negative charge. A demonstration of inductive
effects is readily afforded in the action of the gold-leaf electroscope, Fig.
254, in which two strips of gold-leaf are suspended within a glass case from
wire passing through the top, and terminated in a metal plate. This instrument
is often used for showing the existence of very
small electric charges. Let a stick of sealing-wax
be rubbed and held, say, a foot or more from the
plate of the electroscope, the leaves will diverge
with negative electricity. The sealing-wax being
retained in the same position, touch the plate for
an instant with the finger. This will remove the
negative charge, but the positive electricity will be
retained on the plate by the attraction of the negative
of the sealing-wax. Now remove the sealing-wax,
when the dissimulated charge will spread
itself over the whole insulated metallic portion of
the electroscope, and the leaves will diverge with
a strong charge of positive electricity. If an
excited glass tube is brought near the electroscope,
the leaves will now diverge still more; if
the sealing-wax is replaced in its former position,
the leaves will collapse. In all these cases the
electrified body parts with none of its own electricity
by developing electrical effects in the neighbouring
bodies.
The inductive actions we have described take
place through the air, which is a non-conductor,
and such actions may be made to take place
through any other non-conductor. With solid
non-conductors, such as glass, gutta-percha, &c.,
the inducing body may be brought very near to
the conductor on which it is to act; for the intervening solid substance, or
dielectric, as it has been appropriately called, opposes a resistance to the
combination of the opposite electricities, and the inductive effects are
greatly intensified by the approximation. Faraday discovered that the
amount of inductive action with a given charge is also dependent upon the
nature of the dielectric, and that the electric forces act upon the particles
of the dielectric, circumstances which are of the greatest importance, as
we shall presently find, in practical telegraphy. The most familiar instance
of induction is probably well known to the reader in the Leyden jar, Fig. 255,
which is simply a wide-mouthed bottle of thin glass, covered internally and
externally with tin-foil to within a few inches of the neck. The inner coating
communicates by means of a rod and chain with a brass knob. Such a
jar admits of the accumulation of a larger quantity of electricity than the
conductor of a machine will retain. A very few turns of the machine will
490suffice usually to charge the conductor to the fullest extent; but if it be
put in communication with the knob of a jar, a great many more turns will
be required to attain the same charge in the conductor, and the excess of
electricity represented by these additional turns will have accumulated
within the jar—an effect due to the “dissimulated” electricity of its exterior.
Fig. 255.—The Leyden Jar.
Everybody knows the result when a
metallic communication is established
between the exterior and the interior
of a charged Leyden jar. There is a
very bright spark, a snap, and the jar
is “discharged.” Everybody knows,
also, the sensation experienced when
his body takes the place of the metallic
communication, or forms part of the
circuit through which the communication
takes place. Everybody knows
that the shock then felt may also be experienced
at the same moment by any
number of persons who join hands,
under such conditions that they also
form a part of the line of communication.
Such facts irresistibly suggest
the notion of something passing
through the whole chain, and this
notion is in perfect harmony with the
hypothesis of the “fluids,” for we have only to suppose that it is one or
both of these which rush through the circuit the instant the line of communication
is complete. It was one of Franklin’s discoveries that the
electrical charges of the Leyden jar do not reside in the metallic coatings;
for he made a jar with removable inside and outside coatings, which,
properly taken from the glass, showed no signs of electrification, yet
when replaced the jar was found to be again highly charged. This
would seem to show that the charge clings to, or penetrates within, the
glass.
Let us take a vessel containing water, to which some sulphuric acid
has been added, Fig. 256, and in the liquid plunge a plate of copper,
C, and a plate of pure zinc, Z, keeping the plates apart from each other.
As it is not easy to obtain zinc perfectly free from admixture of other
metals, an artifice is commonly resorted to for obtaining a surface of pure
metal, by rubbing a plate of the ordinary metal with quicksilver, which
readily dissolves pure zinc, but is without action on the iron and other
metals with which the zinc is contaminated, while the quicksilver is not
acted upon by the diluted acid, but is merely the vehicle by which the pure
zinc is presented to the liquid. Under the conditions we have described,
no action will be perceived, no gas will be given off, nor will the zinc dissolve
in the acid. If the electrical condition of the portion of the copper-plate
which is out of the liquid be examined by means of a delicate electroscope,
491it will be found to possess a very weak charge of positive electricity,
and a similar examination of the zinc plate will show the existence on it of
a feeble charge of negative electricity. If the two plates be made to touch
each other, or if a wire be attached to each plate, as shown in the figure,
and the wires be brought into contact outside of the vessel, an action in
the liquid is immediately perceptible at the surface of the copper plate,
when a multitude of small bubbles of hydrogen gas will at once make their
appearance, and the gas will be given off continuously from the copper
plate so long as there is metallic contact through the wires, or otherwise,
between the two plates, or until the acid is saturated with zinc—for in this
action the zinc is dissolving, and, in consequence, liberating hydrogen,
which strangely makes its appearance, not at the place where the chemical
action really occurs, namely, at the surface of the zinc which is in contact
with the acid, but at the surface of the copper which is not acted upon by
the acid.
Fig. 256.—A Voltaic Element.
It is known that when we establish a metallic communication between
two bodies charged with equivalent quantities of positive and negative
electricities respectively, these combine and neutralize each other, and all
signs of electricity vanish. It is obvious that the contact of the two wires
has this effect, as the signs of electric charge which were before discoverable
in each of the plates are no longer found while the wires are in contact.
But the charges reappear the instant the contact is broken, the
chemical action ceasing at the same time. If the wire connecting the two
plates outside of the vessel be carefully examined, it will be found, so long
as the chemical action is going on, to be endowed with new and very remarkable
properties. If this wire be stretched horizontally over a freely
suspended magnetic needle, and parallel to it, the needle will be deflected
from its position, and, if the wire be placed very near it, will point nearly
east and west, instead of north and south. Now, this effect is produced
by any part whatever of the wire, and it instantly ceases if the wire be cut
at any point. These facts at once suggest the idea of its being due to
something flowing through the wire, so long as metallic continuity is preserved.
This idea is much strengthened when we find that the action of
the connecting wire upon the magnetic needle is quite definite—or, in
other words, there are indications which correspond with the notion of
direction. For when the wire, which we shall still suppose to be stretched
492horizontally above the needle and parallel to its direction, is so connected
with the plates immersed in the acid that the portion which approaches
the south-pointing pole of the needle proceeds from the copper plate, while
the portion above the north pole is in connection with the zinc plate, then
the north end of the needle will always be deflected towards the west—whereas,
if the connections be made in the contrary manner, the deflection
will be in the opposite direction; and if the wire be below the needle, the
contrary deflections will be observed with the same connections. The discovery
of the action of such a wire on the magnetic needle was made by
Œrsted in 1819, and it is a discovery remarkable for the wonderful extent
of the field which it opened out, both in the region of pure science and in
that of practical utility.
Fig. 257.—Ampère’s Rule.
Since by such experiments as those just mentioned the notion of a current
is arrived at, the mind recurs to the fiction of the “fluids,” and pictures the
“positive fluid” as rushing in one direction, and the “negative fluid” in
the other, to seek a re-combination into “neutral fluid.” But we must never
lose sight of the fact that these ideas are consciously adopted as representative
fictions to help our thoughts—just as John Doe and Richard Roe,
imaginary parties to an imaginary lawsuit, used to be named in legal documents,
in order to explain the nature of the proceedings. Failing, then, to
find anything really flowing along our wire, it is still absolutely necessary,
seeing there is something definite in its action, to assign a direction to the
supposed current; and it has been agreed that we shall represent the current
as flowing from the positively charged body to the negatively charged
body—that is, in the case we have been considering, from the copper to
the zinc through the wire. When this conventional representation has
been adopted, the action on a magnetic needle can easily be defined and
remembered by an artifice proposed by Ampère. In Fig. 257, let N S represent
the magnetized needle, N being the pole which points towards the
north, and S the south pole. Let C be the end of the wire connected with
the copper plate, and Z that connected with the zinc. The current is therefore
supposed to flow in the direction indicated by the arrows in a wire
above the needle and in the wire placed below. Now, suppose that a man
is swimming in the current in the same direction it is flowing, and with his
face towards the needle, then the north pole of the needle will always be
deflected towards his left. With the direction of current represented in the
figure, the pole, N, will be thrown forward from the plane of the paper, or
towards the spectator.
The reader who desires to study the mutual action of currents and magnets
will find it necessary to fix this idea in his mind. He will now be able
to see that if the wire be coiled round the needle, as shown by the lines and
arrows, Fig. 257, so that the same current may circulate in reverse directions
493above and below the magnet, its effects in deviating the needle will
everywhere concur—that is, the action of each part will be to turn the north
pole towards the left. It is, therefore, plain that if the wire conveying the
current be passed several times round the magnetic needle, the deflecting
force will be increased; and a current, which would, by merely passing
above or below the magnet, produce no marked deflection, might be made
to produce a considerable effect if carried many times round it. The arrangement
for this purpose is shown in Fig. 258, where it will be perceived
that the needle is surrounded by a coil of wire, so that the current circulates
many times about it, and the effects of each part of the circuit concur
in deflecting the needle. Such an arrangement of the wire and needle
constitutes what is called the galvanometer, an instrument used to discover
the existence and direction of electric currents.
Fig. 258.—Galvanometer.
The arrangement of metals and acid which we have described is termed
a voltaic couple, element, or cell; and a great controversy has long been
carried on among men of science as to the place at which the development
of electricity has its origin. Three-quarters of a century ago, the
effect was attributed by Volta to the mere contact of the two dissimilar
metals. In the experiment we have described this contact, supposing the
wires to be of copper, would occur at the junction of the wire and the zinc
plate. Now, by joining the copper plate of such a cell to the zinc plate of
another cell, the copper of that to the zinc of a third, and so on, it is evident
that the number of dissimilar contacts might be indefinitely increased, and
the electric power should be proportionately augmented. It is found that
this is really the case, but Volta’s explanation has been opposed by another
which regards the chemical action in the cells as the real origin of the
electric manifestations. This last explanation, supported by many apparently
conclusive experiments of Faraday and others, has been generally
accepted. Galvanic batteries—as a series of cells joined together in a certain
manner are termed—have been constructed, in which there is no contact
of dissimilar metals; and no electric current can be obtained from an
apparatus in which no chemical action takes place. The contact theory
in a modified form has recently been revived by Sir W. Thomson and
others. In this it is now maintained that some separation of electricities
really does take place by contact of dissimilar substances, but that a
current can be produced only when this separation is continually renewed
by chemical actions. Be the true explanation what it may, the fact is
undoubted that by joining cell to cell, we can really obtain vastly more
powerful effects. If we take a single cell, such as that represented in
Fig. 256, and connect the plates with a long and thin wire, we shall find
494that the current flowing through each part of the circuit is much weaker
than when we connect the plates with a short and thick wire. In other
words, the action in the latter case, when the wire is stretched over a
magnetic needle, will be more powerful than in the former. By using a
long and thin wire the current may be so weakened that it becomes necessary
to surround the needle with many coils of the wire to produce a
marked deflection. Again, much depends upon the material; thus a
copper wire conveys a much more powerful current than a German silver
one of the same dimensions. There thus appears to be a certain analogy
between the flow of electricity along conductors to that of water through
pipes. The longer and narrower are the pipes, the less is the quantity of
water forced through them by a given head; and similarly, the resistance
to the passage of a current increases with the length and narrowness of
the conducting wire. When all other circumstances are the same, the
electrical resistance of a conductor varies directly as its length and inversely
as its sectional area. Hence the current flowing in the apparatus represented
in Fig. 256 would be increased by making the wire thicker, and by
making it shorter by bringing Z and C nearer together, and by making the
area they expose to the liquid larger; for in the liquid also the current
flows as indicated by the arrow, a fact which may be proved by the deflection
of a magnetized needle suspended above the vessel. The magnitude
of the current depends, then, upon two opposing forces, namely, that which
continuously separates the electricities, or drives them apart to re-combine
through the circuit, and that which opposes their passage. The former,
which is termed the electromotive force, originates, according to some, from
the mere contact of dissimilar materials, according to others from the
chemical action. Now, we may increase the strength of the current in a
given arrangement, either by increasing the electromotive force, or by
diminishing the resistance. The increase of the strength of the current,
produced by merely pouring more acid into the vessel, Fig. 256, is due,
according to the chemical theory, to the former cause; according to the
contact theory, to the latter. By multiplying the cells we increase the
electromotive forces: the current receives, so to speak, an onward shove
in each cell, but with each cell we introduce an additional resistance.
Hence, it follows, that when the resistance of the circuit outside of the
cells is extremely small, the current produced by a single cell is as powerful
as that produced by a thousand. But when the external resistance is
great, as when long thin wires are used, the united electromotive forces of
a number of cells are needed to drive the current through the circuit. The
strength of a current, C, is therefore expressible by the following simple
formula, in which r stands for the internal resistance, and e for the electromotive
force in each cell; n represents the number of cells in the battery,
these being supposed exactly similar in every respect; R is the sum of
the resistances in the circuit outside of the battery.
ne
C =
nr + R
It is easily seen that the smaller R is made, the more nearly does the
strength of the current become independent of the number of cells.
Fig. 259.—Daniell’s Cell and Battery.
Fig. 260.—Grove’s Cell and Battery.
But many modifications have been made in the materials and form of the
cells, by which greater power and duration of action have been attained.
Our space permits a description of only two forms, and these must be described
without a discussion of the principles upon which their increased
495efficiency depends. Daniell’s constant cell is represented in Fig. 259, where
D is a battery of ten such cells, A is a cylindrical vessel of copper, C is a
tube of porous earthenware, closed at the bottom, and within it is suspended
the solid rod of amalgamated zinc, B. The copper vessel and the zinc rod
are provided with screws by which wires may be attached. In the copper
vessel is placed a saturated solution of sulphate of copper, and some crystals
of the same substance are placed on the perforated shelf within the vessel.
The porous tube is filled with diluted sulphuric acid. When the battery
is in action the zinc is dissolved by the sulphuric acid, and metallic copper
is continually deposited upon the internal surface of the copper vessel.
Daniell’s battery, in some form or other, is much used for telegraphs and
for electrotyping. Grove’s cell is shown in section in Fig. 260. The
external vessel is made of a rectangular form in glazed earthenware or
496glass. It contains a thick plate of amalgamated zinc, A, A, bent upwards,
and between the two portions a flat porous cell, C, C, is placed, filled with
strong nitric acid, in which is immersed a thin sheet of platinum. The
outside vessel is charged with water, mixed with about ⅛th of sulphuric
acid. D represents a battery of four such cells, in which the mode of connecting
the platinum of one to the zinc of the next may be noticed. The
terminal platinum and zinc form the poles of the battery, and to them the
wires are attached which convey the current. The substitution of plates
of coke for the platinum gives the form of battery known as Bunsen’s, which
is also sometimes made with circular cells. Gover’s and Bunsen’s are much
more powerful arrangements than Daniell’s, but the latter has the advantage
as regards the duration and uniformity of its action.
Fig. 261.—Wire ignited by electricity.
When the current produced by a battery of a dozen or more such cells
is conveyed by a wire, it is observed that this wire becomes sensibly hot,
and, if the wire be thin enough, the heat may be sufficiently great to heat
the wire to redness. By stretching a piece of platinum wire between two
separate rods which convey the current, as represented in Fig. 261, the
length of wire through which the current passes may be adjusted so as to
give any required amount of light, and the wire may even be heated to the
fusing-point of platinum. This property of electricity has some interesting
applications, as, for example, in firing mines and other explosive charges,
and in some surgical operations. A still more interesting exhibition of
heating and luminous effects is observed when the terminals of a battery
of many cells are connected with two rods of coke, or gas-retort carbon.
When the pointed ends of the rods are brought into contact, the current
passes, and the points begin to glow with an intensely bright light, and if
they are then separated from each other by an interval of ⅒th of an inch
or more, according to the power of the battery, a luminous arc extends
between them, emitting so intense a light that the unprotected eye can
hardly support it. This luminous arc is called the voltaic arc, and it excels
all other artificial lights in brilliancy, a fact due to the extremely high
temperature to which the carbon particles are heated, the temperature
being, perhaps, the highest we can attain. It must not be supposed that
in this brilliant light we see electricity: the light is due to the same cause
as the light of a candle or gas flame, namely, incandescent particles of
solid carbon. These particles are carried from one carbon point to the
497other, and it is found that the positive pole rapidly loses its substance,
which is partly deposited on the negative pole. But in order to obtain a
steady light, it is requisite to keep the pieces of carbon at one invariable
distance; and therefore the transference of the material from one pole to
the other, and the loss by combustion, must be compensated by a slow
movement of the carbons towards each other. Several kinds of apparatus
are used for this purpose, but they all depend upon the principle of regulating
the motions by the action of an electro-magnet, formed by the current
itself, which becomes weaker as the carbons are farther apart. The movement
is communicated to the apparatus by clockwork. Duboscq’s electric
lantern is shown in Fig. 262, with enlarged images of the carbon points
projected on a screen. The mechanism of the regulator is contained within
the cylindrical box immediately below the lantern. The supports of
both carbons are moved; that which bears the positive carbon pole being
advanced twice as fast as the other, and thus the light is maintained at the
same level, for the positive carbon wears away twice as fast as the other.
The light is more brilliant when charcoal is used instead of coke, but then
it is necessary to operate in a vacuum, to avoid the combustion of the charcoal.
The voltaic arc has recently been applied to illuminate lighthouses,
and for other purposes, and will probably soon be more widely employed,
for a cheap and convenient mode of producing a uniform current of electricity
has recently been discovered and will be presently described.
Fig. 262.—Duboscq’s Electric Lantern and Regulator.
Fig. 263.—Decomposition of Water.
The current which is maintained by the chemical action taking place in
the cells of the battery can also be made to do chemical work outside of
the battery. When the poles of the battery are terminated by wires or plates
of platinum, and these are plunged into water acidulated with sulphuric
acid, bubbles of gas are seen to rise rapidly from each wire, or electrode,
498as it is termed. Fig. 263 shows an arrangement by which these gases may
be collected separately, and examined, by simply placing over each electrode
an inverted glass tube, filled also with the acidulated water. The
gases collect at the tops of the tubes, displacing the water, and it is found
that from the wire connected with the zinc end of the battery, or negative
electrode, hydrogen gas is given off, while at the positive electrode oxygen
gas is liberated, in volume precisely equal to half that of the hydrogen.
This being the proportion in which these two substances combine to produce
water, it appears that in the passage of the current a certain quantity
of water is decomposed; and the quantity thus decomposed is in reality a
measure of the current, all the other effects of which are found to be proportional
to this. When the electricity in a current is said to be measured,
it is simply the power of the current to deflect a magnet, or the quantity
of gas it can liberate, or some other such effect, which is in fact measured.
The discharge of a Leyden jar through such an apparatus as that represented
in Fig. 263 would present no perceptible decomposition of the
water; yet such a discharge passed through the arms and body produces,
as everybody knows, a painful shock, and is accompanied by a bright spark
and a noise, while the simultaneous contact of the fingers with the positive
and negative poles of the galvanic battery occasions neither shock nor
spark. Thousands of discharges from large jars must be passed through
acidulated water to liberate the amount of gas which a battery current of a
second’s duration will produce. The electricity of the jar is often spoken
about as having a higher tension than that of the battery, but the latter sets
an immensely greater quantity of electricity in motion. The idea may be
illustrated thus: Suppose we have a small cistern of water placed at a great
height, and that this water could fall to the ground in one mass. The fall
of the small quantity from a great height would be capable of producing
very marked instantaneous effects, such as smashing, as with a blow, any
499structure upon which it might fall. This would correspond with the small
quantity of electricity which passes in the discharge of a Leyden jar. Contrast
this with the case in which we allow a very large quantity of water to
descend from a very small height—as when the water of a reservoir is flowing
down a gently inclined channel. It is plain that a different kind of
effect might be produced in this case; the current might be made, for instance,
to turn a water-wheel, which the more forcible impact of the small
quantity of water in the case first supposed would have broken into pieces.
Fig. 264.—Electro-plating.
It is probable that the apparent decomposition of water by the electric
current is in reality a secondary effect, and that it is the sulphuric acid
which is decomposed. When, instead of acidulated water, we place in the
apparatus a solution of sulphate of copper, it is found that metallic copper
is deposited on the negative electrode, and sulphuric acid collects at the
positive electrode. The metal is deposited in a firm and coherent state, and
the useful applications of this deposition of metals are of great interest and
importance. For, in a similar manner, gold, silver, lead, zinc, and other
metals may be made to form thin uniform layers over any properly prepared
surface. The immense advantages which the arts have derived from
electro-plating illustrate in a convincing manner the benefits which physical
science can confer on society at large.
The process of electro-plating may be practised by the aid of apparatus
of very simple character. Fig. 264 shows all that is necessary for obtaining
perfect casts in copper of seals, small medals,
&c. A A is a section of a common tumbler;
B B is a tube, made by rolling some brown
paper round a ruler, uniting the edge with
sealing-wax, and closing the bottom by a
plug of cork, round which the paper may be
tied by a string, or in any other convenient
manner. The tumbler contains a solution of
sulphate of copper, and the tube is filled with
water, to which about one-twentieth of its
bulk of sulphuric acid has been added. A
strip of amalgamated zinc, or a piece of thick
amalgamated zinc wire, is placed in the tube,
and a piece of copper bell-wire is twisted
round the top of it, and has attached to its
other extremity, and immersed in the copper
solution, the article which is to be covered
with copper. We may suppose that this is
to be a cast in white wax or in plaster of
one side of a medal. The cast is carefully
covered with black lead by means of a soft
brush, and the copper wire is inserted in such
a manner as to be in contact with the black
lead at some part. When the apparatus has been left for some hours in
the position represented, a deposit of copper will be found over the blackleaded
surface, and it will be a perfect impression of the wax cast.
Such a copper cast, or any article in copper having a perfectly clean
surface, can be readily covered by a film of silver by means of a similar
arrangement, where a solution of cyanide of potassium, in which some
chloride of silver has been dissolved, is made to take the place of the sulphate
of copper. Electro-plating with the precious metals has become a
500commercial industry of great importance; and this process has completely
superseded the old plan of covering the metallic article to be plated with
an amalgam of silver or of gold, and then exposing it to heat, which volatized
the mercury, leaving a thin film of gold or of silver adhering to the
baser metal. On the large scale a battery of several cells is used for electro-plating,
and the articles are immersed in the metallic solutions as the
negative poles of the battery; any required thickness of deposit being given
according to the length of the time they remain. At the works of Messrs.
Elkington, of Birmingham, these operations are conducted on a grand
scale. The liquid there employed for silvering is a solution of cyanide of
silver in cyanide of potassium, and the positive pole is formed of a plate of
silver, which dissolves in proportion as the metal is deposited on the negative
pole. As the charging of batteries is a troublesome operation, and
their action is liable to variations which affect the strength of the currents,
the more uniform, more convenient, and more economical mode of producing
currents by magneto-electricity, which will presently be described,
has been to a great extent substituted for the voltaic battery.
Fig. 265.—A Current producing a Magnet.
The wire conveying a current not only affects a magnetic needle in the
manner already described, but itself possesses magnetic properties, of
which, indeed, its action on the needle is the result and the indication. If
such a wire be plunged into iron filings, it will be found that the filings are
attracted by it: they cling in a layer of uniform thickness round its whole
circumference and along its whole length, and the moment the connection
with the battery is broken they drop off. This experiment shows that every
part of the wire conveying a current is magnetic, and it may be proved that
the action is not intercepted by the interposition of any non-magnetic
material. Thus the action of the wire upon the magnetic needle takes
place equally well through glass, copper, lead, or wood. Consequently, if
we cover the wire with a layer of gutta-percha, or over-spin it with silk or
cotton, we shall obtain like results on our filings, and if we coil the covered
wire round a bar of iron, while the non-conducting covering of the wire will
compel the current to circulate through all the turns of the coil, it will not
interfere with the magnetic action on each particle of the bar. Whenever
this is done it is found that the iron is converted into a powerful magnet
so long as the current passes. Fig. 265 represents in a striking manner
the result when the current is made to circulate through numerous convolutions
of the wire; and as each turn adds its effect to that of the rest,
magnets of enormous strength may be formed by sufficiently increasing the
501number of the turns. The end of the iron bar is shown projecting from
the axis of the coil, and below it is placed a shallow wooden bowl, containing
a number of small iron nails. The instant the battery connection
is completed these nails leap up to the magnetic pole, and group themselves
round it in the manner shown in the cut; and again, when the current
is interrupted, the iron reverts to its ordinary condition, the magnetism
vanishes, and the nails drop down in an instant. These effects may be
produced again and again, as often as the current flows and is broken. A
magnet so produced is called an electro-magnet, to distinguish it from the
ordinary permanent steel magnets. By coiling the conducting wire round
a bar of iron which has been bent into the form of a horse-shoe, very
powerful magnets may be produced, and enormous weights may be supported
by the force of the magnetic attraction so evoked. Fig. 266 represents
the apparatus for experiments of this kind, in which weights exceeding
a ton can be sustained.
Fig. 266.—An Electro-magnet.
Here, then, we have a striking instance of the subtile agent electricity,
evoked by the contact of a few pieces of zinc with dilute acid, showing itself
capable of exerting an enormous mechanical force. Engines have
been constructed in which this force is turned to account to produce rotatory
motion as a source of power. Such engines have certain advantages
for special purposes; but the money cost for expenditure of material for
power so obtained is, at least, sixty times greater than in the case of the
steam engine. It is, however, in producing mechanical effects at a distance
502that the electric current finds the most interesting practical application
of its magnetic properties. These are the actions which are so extensively
utilized in the construction of telegraphic instruments, of clocks
regulated by electric communication with a standard time-keeper, and
of many ingenious self-registering instruments. The telegraph will be
described in the next article, and we shall also have occasion in subsequent
articles to describe some of the other applications of electro-magnetic
and electro-chemical force.
These very remarkable phenomena were discovered by the illustrious
Faraday, in 1830, and this discovery, and that of magneto-electricity,
may be ranked among the most memorable of his many brilliant contributions
to electric science. Let two wires be stretched parallel and very near
to each other, but not in contact. Let the extremities of one wire, which
we shall term A, be connected with a galvanometer (page 415), so that the
existence of any current through the wire may be instantly indicated. Let
the two extremities of the other wire, B, be put into connection with the
poles of a battery. The moment the connection is complete, and the
battery current begins to rush through B, a deflection of the galvanometer
needle will be observed, indicating a current of very short duration through
A in the opposite direction to the battery current through B. This induced
current, which is called the secondary current, does not continue to flow
through A: it occurs merely at the time the primary or battery current is
established; and though the latter continues to flow through the wire, B, no
further effect is produced in the other wire. When, however, the battery
connection is broken, and the primary current ceases to flow, at that instant
there is set up in the wire, A, another momentary secondary current, but
this one is in the same direction as the battery current. This is termed the
direct secondary current, in opposition to the former, which is called the
inverse current.
These effects are much more powerful when, instead of lengths of straight
wire, or single circles of wires, we use two coils of wire, one of which,
namely, that which conveys the primary currents, is placed in the axis of
the other. It must be distinctly understood that the secondary currents
are of momentary duration only; they are not produced at all while the
battery is flowing, but only at the time of its commencement and cessation.
If, however, we make the primary coil so that it can be slid in and out of
the axis of the other, then while the primary current is continuously flowing,
we can produce secondary currents in the other coil, by causing the
coils to approach or recede from each other. As we bring the coils near
each other, and slide the primary into the secondary, the current in the
latter is inverse; when the one coil is receding from the other, it is direct.
These mechanical actions are not produced without expenditure of force,
for the approaching coils repel each other and the receding coils attract
each other. The setting up of the battery current in the primary coil when
placed within the other is equivalent to bringing it, with the current flowing,
from an immense distance in an extremely small time. Similarly,
503when the battery current is broken, it is equivalent to an instantaneous
recession. The effects, therefore, are proportionately powerful. It is found,
also, and this we shall presently refer to more fully, that when, instead of
the primary coil, a magnet is similarly moved into, or removed from, the
axis of the secondary coil, currents in opposite directions are set up in the
latter without any battery being used at all. The direction of these currents
is the same as would be produced by a primary current that would form,
in a piece of iron placed in the axis of the coil, an electro-magnet with
poles similarly situated to those of the magnet so introduced or withdrawn.
Hence, by placing a bar of soft iron in the axis of the primary coil, the
secondary currents will be produced with increased force. When a long
secondary coil, having the turns of its wire well insulated from each other,
surrounds a primary coil provided with a core of soft iron, or still better,
with a bundle of annealed iron wires, a series of powerful discharges, like
those of a Leyden jar, may be obtained between the terminals of the
secondary coil, when the battery contact is made and broken in rapid
succession.
Fig. 267.—Ruhmkorff’s Coil.
Such induction coils have been very carefully and skilfully constructed by
Ruhmkorff, and are therefore often called “Ruhmkorff’s Coils.” One of these
is represented in Fig. 267. A B is the coil, and the apparatus is provided
with what is termed a condenser, which consists of layers of tin-foil placed
between sheets of thick paper, and alternately connected so that one set
communicates with one extremity of the primary coil, and the other with
the other. This condenser is conveniently contained in the wooden base
of the instrument. Its introduction has greatly increased the intensity of
the secondary current, and sparks of 18 in. or 20 in. in length have been
obtained in the place of very short ones.
It should be stated that of the two secondary currents, only one has
sufficient intensity to traverse the secondary circuit when there is any break
in its continuity. This is the direct secondary current, or that which is
produced on breaking the primary circuit. The reason is that the commencing
current in the primary circuit induces in the spires of its own coil
an inverse current, and the battery current therefore attains its full strength
gradually, but still in a very short time; while, on the cessation of the
battery current, the same induction sends a wave of electricity through the
primary coil in the same direction, and then the current ceases abruptly.
Consequently, in the latter case, the induced electricity of the secondary
coil is set in motion in much less time, and therefore possesses much greater
intensity.
504The magnetism of the iron core is usually made use of to break and
make the current, by the attraction of a piece of iron attached to a spring,
which, by moving towards the end of the core, separates from a point in
connection with the battery, and, the current no longer flowing, the magnetism
ceases, and the spring again brings back the iron and renews the
contact.
Fig. 268.—Discharge through Rarefied Air.
By means of such coils many surprising effects have been produced.
Perhaps one of the most beautiful experiments in the whole range of physical
science is made by causing the discharges of the secondary coil to take
place through an exhausted vessel in the manner represented in Fig. 268.
A beautiful light fills the interior of the vessel, and the terminals appear
to glow with a strange radiance—one being surrounded with a kind of blue
halo and another with a red. On reversing the direction of the currents,
which is done by the little apparatus at the right-hand end of the coil in
Fig. 267, the blue and the red radiance change places. Beautiful flashes of
light may also be made to appear in the vessel, having the most marked resemblance
to the streamers of the Aurora Borealis. When, instead of vessels
almost free from common air, we repeat the experiment with tubes containing
an extremely small residue of some other gas, such as hydrogen,
carbonic acid, &c., the colour of the light and other appearances change
506Geissler’s tubes have already been spoken of in connection with the spectroscope;
but, independently of that, the various beautiful appearances
which such tubes have been made to present, by the introduction of fluorescent
substances and other devices, render the induction coil an instrument
of the highest interest to the scientific amateur. Then there are striking
physiological and other effects which the coil is capable of producing. For
instance, we are able by its instrumentality to produce from atmospheric
air unlimited quantities of that singular modification of oxygen which is
called ozone. The electricity of the coil has been used for firing mines,
torpedoes and cannons, and for lighting the gas-burners of large buildings.
Fig. 268a.—Large Induction Coil at the old Polytechnic Institution, London.
The late Mr. Apps, who was well known as a skilful constructor of
scientific apparatus, devoted much attention to improving the induction
coil, and he made a very large one for the Polytechnic Institution in
Regent Street, London, which Institution was at that time the home of
popular science, under the direction of Mr. Pepper. This coil is represented
in Fig. 268a, surrounded by the somewhat scenic accessories
which were then supposed to be required for making science
attractive to the multitude. Externally, the coil appeared as a cylinder,
nearly 5 feet long and 20 inches in diameter. From each end projected
smaller cylinders. All these and also the two upright pillars upon which
the apparatus was supported were covered with ebonite. The large
cylinder contained the primary coil, which was made of copper wire one-tenth
of an inch in diameter and 3,770 yards long, covered with cotton
thread, and making about 6,000 turns round the central core. This
primary coil was inclosed in an ebonite tube ½-inch thick, and outside of
the tube, occupying 4 feet 2 inches of its length, was the secondary coil,
containing 150 miles of silk covered wire, ·015 inch diameter, and very
carefully arranged for insulation, so as to resist the tension of the electricity
when the coil was in action. The condenser contained 750 square feet
of tin-foil, and 40 Bunsen cells supplied the current for the primary coil.
The power of this instrument was very great, for it would give a spark
through the air of more than two feet in length, and the discharge could
perforate a certain thickness of glass. It would charge a battery of Leyden
jars having 40 square feet of tin-foil by only three breaks of contact in the
primary circuit, so that the discharge would deflagrate considerable
lengths of wire. The appearance of the spark, with this, as with other
large induction coils, may be described as a thick line of light, surrounded
by a reddish halo of less brilliancy, and this halo, unlike the line of the
spark, had a sensible duration. The reddish glow might be blown aside
by a current of air when a series of discharges was taking place, and
partly separated from the denser looking line of light. The latter is no
doubt formed by intensely heated particles of the metals between which
the discharge takes place, while the former is probably due to the incandescence
of the oxygen and nitrogen gases in the air. The disc shown in
our illustration behind the coil was for carrying six Geissler tubes, to display
the pretty experiment of the various colours of the luminous discharge
in different attenuated gases. When the coil was first mounted it was
provided with an ordinary contact-breaker, but as the strong sparks were
found to very soon destroy the contact points, a contact-breaker was substituted
on Foucault’s plan. In this, the contacts are made by a platinum
tipped wire dipping into mercury, that occupies the bottom of a strong
glass vessel and forms part of the circuit. The vessel is filled with alcohol,
which is a non-conductor, and it is therefore in the midst of this liquid
507that the contacts are made and broken. This apparatus is shown in the
illustration, on the table at the left. A favourite experiment at the Polytechnic
was to connect one of the discharging wires of the coil with the
back of a large looking-glass, and bring the other wire to the front. In
this case the sparks assumed a peculiar appearance, for they became thin
and wiry-looking, and divided into many branches. They were very
bright, and the noise of the discharges, was crackling and quite different
from that produced by the blow of the flaming sparks taken through the
air. Their appearance is represented in Fig. 269. The effects in this
experiment were probably due to
the spark taking a path on the
surface of the glass determined
by points of moisture or other
inequalities.
Fig. 269.—Spark on the Looking-glass.
Ruhmkorff’s coil has been of
great advantage to the electrician,
for it supplies a stream of high
tension electricity like that of
the common machine, but more
readily and conveniently. M.
Ruhmkorff was the first person to
obtain the great prize of £2,000,
which the late Emperor of the
French (Napoleon III.) directed,
in 1852, should be awarded every
five years for the most useful application
of the voltaic battery.
But no award had been made
until 1864, when the inventor of
the induction coil was properly
considered worthy of it. This invention
was the means of bringing
into notice a new range of interesting
phenomena, especially
those attending the discharge passed through highly exhausted vessels.
Investigations into the circumstances which modify the appearances, and
especially into the nature of the stratified discharge in which the vessels are
filled with bands or flakes of light separated by dark intervals, have long
engaged the attention of some of our ablest physicists. Remarkable results
were obtained by Mr. Crookes with very highly exhausted vessels. These
showed not only beautiful fluorescent luminous effects, but in them the
discharge could produce mechanical actions, and Mr. Crookes was led to
regard it as a stream of radiant matter.
When it had been shown that an electric current was capable of
evoking magnetism, it seemed reasonable to expect that the reverse
operation of obtaining electric currents by means of magnets should be
possible. Faraday succeeded in solving this interesting problem in November,
1831, and one of his earliest, simplest, and most convincing experiments
508for the demonstration of the production of electricity by a magnet
is represented in Fig. 270. A B is a strong horse-shoe magnet, C is a
cylinder of soft iron, round which a few feet of silk-covered copper wire are
wound; one end of the wire terminates in a little copper disc, and the other
end is bent, as shown at D, so that it is in contact with the disc, but pressing
so lightly against it that any abrupt movement of the bar causes the
point of the wire and the disc to separate. When the bar is allowed to
fall upon the poles of the magnet, the separation occurs, and again when
it is suddenly pulled off; and on each occasion a very small but brilliant
spark is observed where the contact of the wire and disc is broken. It
was in allusion to this experiment that a contributor to “Blackwood’s
Magazine” wrote:
Around the magnet, Faraday
Is sure that Volta’s lightnings play;
But how to draw them from the wire?
He took a lesson from the heart;
‘Tis when we meet, ‘tis when we part,
Breaks forth the electric fire.
Fig. 270.—Magneto-electric Spark.
Fig. 271.—A Magnet producing a Current.
Fig. 272.—Clarke’s Magneto-electric Machine.
If a coil of fine insulated wire be passed many times round a hollow
cylinder, open at the ends, and the extremities of the wire connected with
a galvanometer at some distance, then if into the axis of the coil, A B,
Fig. 271, a steel magnet be suddenly introduced, an immediate deflection
of the needle takes place; but after a few oscillations it returns to its former
position. When the magnet is quickly withdrawn, the needle receives a
momentary impulse in the opposite direction. The magnetization and demagnetization
of the iron core in the induction coil would, therefore, of
itself cause the induced currents already described, for these actions are
equivalent to sudden insertion and withdrawal of a magnet. If we suppose
509C, in Fig. 271, to represent, not a magnet, but a piece of soft iron—the
reader will remember that this soft iron can be, as often as required, magnetized
and demagnetized by simply bringing near one end of it the pole
of a permanent magnet (see page 484). Upon this principle many ingenious
machines have been constructed for producing electric currents by the
relative motions of magnets and of soft iron cores surrounded by wires.
510Clarke’s machine is shown in Fig. 272. A is a powerful steel magnet
fixed to the upright. A brass spindle passing between the poles can be
made to rotate very rapidly by the multiplying-wheel, E, on which a handle
is fixed. There are two short cylinders of soft iron parallel to the spindle,
united together by the transverse piece of iron, D, which turns with the
spindle. Each bar is surrounded by a great length of insulated copper
wire, and the ends of the wires are so connected with springs which press
against a portion of the spindle, which is here partly formed of a non-conducting
material, that the currents generated in the coils, although in
different directions as they approach a pole and recede from it, are nevertheless
made to flow in one direction in the external circuit. R R in the
figure represent two brass handles, which are grasped by a person wishing
to experience the shocks the machine can give when the wheel is
turned. When the terminals of the coil are provided with insulating
handles and connected with pointed pencils of charcoal, the electric light
can readily be produced by expenditure of mechanical effort in turning the
handle. The arrangement of the points for this purpose is shown in Fig.
273, and we shall presently see what advantage has been drawn from this
experiment on a great scale as a source of light.
Fig. 273.—Magneto-electric Light.
It will be observed that during the revolution of the armatures, as the
wire-covered iron cores are termed, there are two maximum and two
minimum points at which the currents are strongest and weakest. These
variations may be lessened by increasing the number of armatures and
of magnets, and Mr. Holmes arranged a machine with eighty-eight coils
and sixty-six magnets, and the connections were so contrived that the
currents always flowed in the same direction in the external circuit. This
machine required 1¼ horse-power to drive it when the currents were flowing,
but much less when the circuit was interrupted, and it was designed for,
and successfully applied to, the production of the electric light for lighthouse
illumination. Instead of steel magnets which gradually lose their
strength, it is obvious that electro-magnets might be employed, but this
source of electricity is costly, troublesome, and inconstant. Mr. Wilde hit
upon the idea of using a small magneto-electric machine with permanent
steel magnets, to generate the current for exciting a larger electro-magnet,
and the current from this produced a still more powerful electro-magnet,
511from which a magneto-electric current could be collected and applied.
The same idea was subsequently applied in other forms, as by shunting off
a portion of the current produced from the mere residual magnetism of an
electro-magnet, to pass through its own coils and evoke a stronger magnetism,
which again reacts by producing a more powerful current, and so on
continually; the limit being dependent only on the mechanical force employed,
and on the power of the wires to convey the electricity, for they
become very hot, and, unless artificially cooled, the insulating material
would be destroyed. The armatures used in Wilde’s, Ladd’s, and other
machines of this kind, are quite different in arrangement from those of
Clarke’s machine, and are far superior. They are formed of a long bar of
soft iron, of a section like this, Ꮋ, and the wire is wound longitudinally
between the flanges from end to end of the bar, up one side and down the
other. This armature rotates about its longitudinal axis between the pairs
of the poles of a file of horse-shoe magnets, either permanent, or electro-magnets
excited by the magneto-electric currents. In this case opposite
poles are induced along the edges of the bar, and these poles are reversed
at each half-turn. The intensity of the induced currents increases with
the velocity with which the armature is made to revolve up to a certain
point; but because the magnetization of the soft iron requires a sensible
time to be effected, and the poles are reversed at every half-turn, it is
found that a speed increasing beyond the limit is attended by decrease of
the intensity of the current. The intensity in such machines has, therefore,
a definite limit. But in a modification of the magneto-electric machine,
which has quite recently been invented by M. Gramme, the limit is vastly
extended by the ingenious disposition of the iron core and armatures, and
his machines appear to solve the problem of the cheap production of steady
and powerful electric currents, so that electricity will soon be applied in
processes of manufacture where the cost of electrical power has hitherto
placed it out of the question. We shall now endeavour to explain the
principle on which the Gramme machine depends, and describe some forms
in which it is constructed.
Fig. 274.
Fig. 275.—Gramme Machine for the Laboratory or Lecture Table.
Let X, Fig. 274, be a coil of covered wire; then while a bar magnet, B A,
is advancing towards it and passing through it, as at M, a current will
flow through the coil and along a wire connecting its ends, s s. The current
will change its direction as the centre of the magnet is leaving the coil
512to advance in the direction, B A. If A A´ be a bar of soft iron, with the coil
fixed upon it, we can still excite currents in the coil by magnetizing the bar
inductively. If the pole of a permanent magnet be carried along from A´
to M in a direction parallel to the bar, but not touching it, the part of the
bar immediately opposite will be a pole of opposite name, and the advance
of this induced pole towards M will be attended with a current in the coil,
and its recession by an opposite current. It need hardly be mentioned
that the same result is attained if the magnetic pole is stationary, and the
bar with the coil upon it moved in proximity to it. Now imagine that the
bar is bent into a ring, the ends, A A´, being united. If the ring be made to
turn round its centre in its own plane, and near a magnetic pole, it is plain
that when the coil is approaching this pole a current will be produced in it,
and when it is receding, an opposite current. Let the number of coils be
increased, and each coil in turn will be the seat of a current, or of the electrical
state which tends to produce a current. In Fig. 275 the reader may
see how this disposition is realized. The figure shows a form of the Gramme
Machine adapted for the lecture-table or laboratory. A M´ B M is the soft
iron ring, covered with a series of separate coils placed radially, O is a compound
horse-shoe steel magnet, S its south pole, N its north pole, each pole
being armed with a block of soft iron hollowed into the segment of a circle
and almost completely embracing the circle of coils. The magnetism of each
pole is strongly developed in the interior faces of these armatures. The inductive
action tends to produce two equal and opposite currents, which, like the
currents of two similar voltaic batteries joined by their like poles, neutralize
513each other in the connected coils, but flow together through an external
circuit. Fig. 276 will make clear
the manner in which the coils,
B B, are placed on the ring, A.
The length of wire in each coil
is the same, and the extremities
are attached to strips of
copper, R R, which are fixed
on the spindle of the machine.
The two ends of each wire are
connected with two consecutive
strips, while the coils are
insulated from each other, and
thus each coil, like the element
of a battery, contributes to the
aggregate current. The currents
are drawn off, as it were,
from these axial conductors at
two opposite points of the ring,
by springs very lightly touching
them on each side of the
spindle, as may be seen in Fig. 275. In Fig. 277 is another arrangement of
the table apparatus with the magnet vertical, and formed according to the
new plan suggested by M. Jamin, who finds the best magnets are made by
tying together thin strips of steel.
Fig. 276.—Insulated Coils surrounding an Annulus of Iron Wires.
Fig. 277.—Hand Gramme Machine, with Jamin’s Magnet.
514But the importance of this invention consists in the facility which it
affords for cheaply producing electricity on a scale adapted for industrial
operations, for the deposition of metals, for artificial light, and for chemical
purposes. The great importance of a cheap electric light for lighthouses
prompted the British Government to permit the inventor to exhibit the light
thus produced from the Clock Tower of the Houses of Parliament; for the
signal light during the sittings of the House had previously been produced
by a gas-light. This electric light was produced by a powerful Gramme
machine, such as that shown in Fig. 278, driven by a small steam engine
in the vaults of the Houses of Parliament, and the ordinary carbon points,
reflectors, &c., were used in the Clock Tower, where the light was exhibited;
copper wire ½ inch diameter being used to convey the current from the
machine to the carbons. The result of these experiments may be gathered
from the following extract from an official report made by the engineers of
the Trinity House:
“Pursuant to the instructions received from the Deputy Master to furnish
you with my opinion on the relative merits of the electric and gas
lights under trial at the Clock Tower, Westminster, I beg to submit the
following report:—On the evening of the 1st ultimo I was accompanied
by Sir F. Arrow (who kindly undertook to check my observations by his
experience) to the Westminster Palace, where we met Captain Galton, R.E.,
Dr. Percy, and some gentlemen connected with the electric and gas apparatus
under trial. I was informed that the stipulations under which the
lights were arranged were, that they be fixed white to illuminate a sector
of the town surface of 180°, having a radius of three miles. I first examined
the Gramme magneto-electric machine, in use for producing the
currents of electricity. This machine we found attached by a leather
driving-belt to the steam engine belonging to the establishment. We then
proceeded to the Clock Tower, where we found the electric lamp, at an
elevation of 250 ft. The Wigham gas apparatus was placed at the same
elevation, within a semi-lantern of twelve sides, about 8½ ft. in diameter,
and 10 ft. 3 in. high in the glazing. Near the centre of the lantern were
three large Wigham burners, each composed of 108 jets. After the examination
of the apparatus, we proceeded to Primrose Hill, for the purpose
of comparing the electric and gas lights at a distance of three miles. The
evening, which was wet and rather misty, was admirably suited to our
purpose, ordinary gas-lights being barely visible at a distance of one
mile.”
The results of a photometric comparison of the electric and gas lights
were as under, the machine making 389 revolutions per minute, and absorbing
2·66 horse-power; the illuminating power of the gas used being 25
candles, and the quantity consumed 300 cubic ft. per hour.
Electric Light.
Wigham Gas Burner. 108 jets.
Relative intensity of lights
945·56
370·56
Or as
100
39·19
Illuminating power in standard sperm candles as units
3,066
1,199
515“Electric Light.—Total cost per session £174 5s. 0d., being equal to
5s. 7d. per hour of exhibition of the light. Details shown in the full report.
Gas Light.—Total cost per session of one burner of 108 jets, £159 15s. 3d.,
equal to 5s. 1·4d. per hour of exhibition of light, and £296 3s. 4d., equal
to 9s. 5·9d. per hour of exhibition of the light, when using three burners of
108 jets each. Details shown in the full report. It will be observed from
the photometric measurements, before referred to, of the electric light and
108–jet gas burner, that in the case of the electric light we have at our disposal
for distribution over the required area an illuminant radiating freely
in space equal to 3,066 candles; with the gas light we have an illuminant
radiating freely in space equal to 1,199 candles. It is to be remembered
that in dealing with the small electric spark as the focus of a dioptric apparatus
for distribution over the required area, the light can be more perfectly
utilized than with the large gas flame of the Wigham burner, owing to
its very small dimensions as compared with the latter. The relative cost
and efficiency of the three modes of illumination may be summed up as
follows:
Electric Light.
Gas.
One 108–jet
Three 108–jet
Burner.
Burners.
Cost of light per hour, in pence
67
61·4
113·9
Or as
100
91·6
170
Cost of light per candle per hour in pence
·0219
·0512
·0317
Or as
100
233·8
144·7
Cost of light from a dioptric apparatus for fixed light per standard candle per hour expressed in pence
·00118
·00310
·00275
Or as
100
262·7
233·1
“Thus by adopting the electric light as a standard of intensity and cost,
there is shown a superiority over the gas in intensity of 65·2 per cent. when
using one 108–jet burner, and 27·1 per cent. when using three 108–jet
burners. There is also shown a saving in cost per candle or unit of light
per hour of 162·7 per cent. when using one 108–jet burner, and 133·1 per
cent. when using three of these burners, forming a triform gas-light. It
is further to be remembered that the triform gas-light actually represents
the maximum power obtainable at present by gas; but no reference has
been made to the power of increase capable in the electric light by the
adoption of two magneto-electric machines. By having the machine and
lamp in duplicate, as estimated, and which I consider a necessity to insure
perfect confidence in the regular exhibition of the electric light, this light
can be doubled in intensity during such evenings as the atmosphere is
found to be so thick as to impair its efficiency. This double power would
be obtained at the trifling additional cost of coals and carbons consumed
during the time this increased power may be found to be necessary; this
additional cost I estimate at 4d. per hour. With the arrangement proposed
516for the electric light, I consider this powerful illuminant, if manipulated by
517careful attendants, perfectly reliable: in proof of this I may state that the
electric light at the Souter Point Lighthouse, on the coast of Durham, has
now been exhibited two years and a half, and the light has never been
known to fail for one minute.”
Fig. 278.—Gramme Machine, with Eight Vertical Electro-magnets.
Fig. 279.—Gramme Machine, with Horizontal Electro-magnets.
Fig. 278 represents one of the light-producing machines. The electro-magnets
are excited by a portion of the currents they themselves produce,
they retaining sufficient residual magnetism to develop the currents.
There is a pair of current-collectors on each side. This machine weighs
1,540 lbs., its height is 3 ft., and width 2 ft. It will produce a light having
the intensity of 500 Carcel lamps, which may be doubled by increasing the
speed. Fig. 279 is another form which is also adapted for illuminating purposes,
and, when made with fewer coils, for electrotyping purposes also.
There are in this also two sets of current-collectors, and by means of a
connecting cylinder (seen at the base of the machine) the currents can be
combined for quantity and for tension as may be required. This machine
is only about 2 ft. square, and it produces a light equal to 200 burners;
but this may be increased, as the following table shows:
518
Number of revolutions per minute.
Intensity of light in Carcel Lamps.
Remarks.
650
77
No heating and no sparks.
850
125
No heating and no sparks.
880
150
No heating and no sparks.
900
200
No heating and no sparks.
935
250
A little heat, no sparks.
1,025
290
Heat and sparks.
The value of M. Gramme’s invention for electro-plating is proved by the
fact of its adoption by Messrs. Christofle of Paris, whose electro-plating
establishment is one of the largest in the world. This firm has no fewer
than fourteen of these machines at work, and each is capable of depositing
74 ozs. of silver per hour. There is little doubt that the electric current
will now soon be employed for reducing metals. Thus fine copper, which
is worth 3s. or 4s. per lb., may perhaps be obtained at about the cost of
ordinary copper; potassium, sodium, and aluminium at less than half their
present price; and magnesium, calcium, and other rare metals at prices
which will bring them into commercial use. The machine shown in Fig.
280 is intended for electro-plating and for general purposes: it supplies the
means of readily and cheaply plating with copper, or with any other metal,
such articles as steam pipes, boiler tubes, ship plates, guns, bolts, nails,
marine engines, machinery, culinary vessels, cisterns, &c. The advantage of
protecting iron or other material from corroding agents is obvious; and as
iron coated with copper is available not only for useful, but also for artistic,
purposes, as a cheap substitute for bronze, this invention will doubtless
lead to a greatly extended application of bronzed iron in buildings and
ornamental structures.
The machine well illustrates how mechanical work may be changed into
electricity, and electricity caused to do work. The power required to
drive the machine at a given speed is much less when no current is being
drawn from it, than when the current is flowing. If the current from one
machine is sent through the armature of another, the latter revolves, and
may be made to do work. Thus power may be conveyed to a distance by
electricity, with only the loss caused by the resistance of the conducting
wires. If, when two machines are thus connected, the direction of rotation
in the first one be suddenly reversed, the armature of the second will
almost immediately stop, and then resume its motion in the opposite direction.
A very interesting experiment can be performed when the circuit
connecting the two machines is made to include a certain length of platinum
wire. When both machines are in motion, the platinum exhibits no heating
effects; but if the second machine be stopped by an assistant while the
rotation of the first is continued, the wire is raised to a red heat. In this
way it is shown that motion, electricity, and heat are related to each other,
and are mutually convertible; for on the stopping of the second machine,
the electricity being no longer used up, so to speak, in producing motion,
has its power transformed into heat.
The Gramme machine has also been ingeniously employed for railway
brakes on some of the Belgian lines; and it is applicable to telegraphy,
where the cost of zinc, acids, batteries, &c., is a considerable item. It is
519impossible to predict the many applications for manufacturing purposes
which will be made of electricity, now a cheap, reliable, and convenient
mode has been discovered of producing currents of any required strength.
Though by no means the first or only machine by which mechanical force
can be converted into dynamical electricity, it shows an immense advance
on any former one in the regularity of the action, and in the capability
of being driven at a very high rate of speed without the inconvenient
accompaniments of the heating of the conductors and destructive sparks
at the movable contacts. There can be no doubt of the importance of this
machine for use in lighthouses, and for metallurgical and chemical purposes,
and the inventor believes the time will come when all large ocean-going
vessels will carry an electric light at the masthead. The light would
be sufficiently powerful to show rocks or land five or six miles ahead, and
an additional safeguard of incalculable value would be thus provided for
those “that go down to the sea in ships, that do business in great waters.”
Fig. 280.
Fig. 280a.—The Alliance Machine.
It was mentioned in the last section that the introduction of so convenient
and reliable a means of producing electrical currents as the
Gramme machine, would cause electricity to be largely applied for
illuminating and other purposes. The Gramme machine was first made
in 1870, and it attracted much attention, as the principle of combining the
currents was quite different from that used in previous magneto-electric
520machines. In fact, the Gramme machine yielded quite unexpected results,
and the principle employed in it opened a new field. The development
that has taken place in the applications of electricity within the twenty
years since 1870 has been truly marvellous. The electric light appears
to have been first used in lighthouses about 1862, and the machines by
which the current was produced were, in principle, combinations of a
great number of Clarke’s machines (see page 509). One such machine
was invented by Mr. Holmes, and was used for the illumination of the
South Foreland Lighthouse in 1862. Another similar form of still earlier
invention had been set up in Paris as early as 1855,—not, indeed, for the
purposes of illumination, but for a project which failed. Its arrangement
had been originally suggested by a Belgian physicist in 1849; and the
machine of 1855, having received certain improvements, afterwards became
very well known by the name of the Alliance Company’s machine, or simply
the Alliance machine. It is represented in its improved form in Fig. 280a.
Here ranges of steel horse-shoe magnets will be observed, each magnet
weighing about 40 lbs. and made of six plates of tempered steel, held
together with screws. Each of the eight rows of magnets contains
seven, and thus sixteen poles are presented at uniform distances, arranged
in circles. Carried on the central axle are six discs, which revolve between
the circles of sixteen poles, and on the circumference of each disc are
sixteen equidistant bobbins or coils of insulated wire, so that the whole of
the sixteen coils are opposite to the sixteen poles at the same moment.
The extremities of the wires at the coils are connected with proper
521adjustments for gathering up the currents, and by means of these the
coils may be arranged either for tension or for quantity, like the elements
of a battery (page 494).
Fig. 280b.—Wilde’s Machine.
Wilde’s machine, which has been mentioned in page 511, is shown in
fig. 280b. It will be observed that this consists of a small machine, M, with
permanent steel magnets, and the current from these circulates through
the coils of the electro magnets, A B. The arrangement of the armatures,
bobbin, commutators, etc., is the same in both cases. But as
a speed of 2,500 revolutions per minute was needed, it was necessary to
522keep the bearings, T T, from heating by causing cold water to circulate
through them. Mr. Ladd arranged a machine on the same principle as
Wilde’s, by suppressing the permanent magnets, but availing himself of
the residual magnetism of the iron core to bring about the induction.
A machine of this kind was shown at the Paris Exhibition of 1867, and
people were quite astonished to see electrical power capable of producing
a brilliant light developed by a small machine 2 ft. long, 1 ft. wide,
and 9 in. high. But the great velocity of rotation, and the consequent
heating of the bearings, left much to be desired before a really practical
machine could be produced.
Fig. 280c.—Siemens’ Dynamo.
In the newest Siemens’ machine, represented in fig. 280c, the Gramme
principle is made use of, as the revolving coil is of large diameter, and
it consists of a copper cylinder, on which are wound a number of
juxtaposed coils like those of a galvanometer. The revolving cylinder is
surrounded by the poles of a system of electro-magnets excited by the
whole of the induced current being passed through their coils. In a
paper describing this machine, Siemens first made use of the term
“dynamo-electric machine,” and this expression, contracted to the
single word DYNAMO, has since been universally employed to designate
machines of this kind. The modifications in the forms and arrangements
of the different dynamos that have been invented in late
years are endless, and every week patents are granted for further
improvements and fresh combinations of the parts. It would be
quite beyond the scope of this work to enumerate all the forms of the
dynamo that have been favourably spoken of; but we shall content ourselves
by adding a drawing of the Brush dynamo (Fig. 280d), which has
been so largely used for electric lighting in the United States. In this
dynamo we have a Gramme ring, but the number of coils on it is reduced
523to eight, the intervals being filled up with pieces of iron, and the ring
revolves in a vertical plane between the poles of two double oblong electro-magnets,
which are arranged with poles of the same name opposite to
each other. The commutators shown in the nearer part convert the alternately
reversed currents generated in the coils into a direct continuous
one. They are formed with bundles of wires, as in the Gramme machine.
Fig. 280d.—The Brush Dynamo.
Fig. 280e.—Siemens’ Regulator.
But the providing of a cheap and efficient source of current electricity,
although an absolutely necessary step, would not have been capable of
bringing about the present development of electric lighting, unless the
appliances by which the current is made to manifest itself as light had
not also been brought nearly to perfection. The conditions required to
maintain a steady light from a current of electricity passing between
carbon points have been already explained on page 497, and a representation
of Dubosc’s electric lantern and regulator is shown. The regulator
systems that have been invented since it became obvious that the light of
the electric arc admitted of practical application on the large scale are
very numerous. The earlier forms of regulator, which were used only for
scientific purposes—such as lantern projections on screens, experiments
on light, etc.—were complicated in their arrangements and uncertain in
their action, for great variations in the light sometimes took place, and
occasionally it would, indeed, be extinguished, and then again shine out
as brightly as before. Nearly all the regulators that have come into use
depend upon movements controlled by electro-magnetic actions produced
automatically as the distance between the carbon changes. It would,
however, lead us too far into the technicalities of the subject to explain
minutely the mechanism of any particular form of the mechanical regulators,
and the results depend so often upon the minute details, that it
would be difficult to trace the action without a set of large and complete
drawings. Perhaps the regulators that have been most used are those of
Serrin, Siemens, Brush, Thomson, Houston and Edison. But nearly
every inventor has produced different forms of his apparatus; Siemens,
for instance, has patented eight or ten regulators. Fig. 280e shows the
mechanism of one of the last named inventor’s regulators, in which the
524two actions required for the separation and approach of the carbons are
determined respectively by the vibrations of the rocking lever, M Y L,
actuated by the electro-magnet, E, and the simple weight of the upper
carbon-holder, A A. When the lamp is not in circuit, the lever, L, is thrown
back by a spring, the tension
of which is regulated by the
screw, R, so that the catch,
Q, is disengaged from the
wheel, I. The train of wheels
is then free to revolve by
action of the rack, A, supporting
the weight of the
upper carbon, until the
motion stops by the carbons
touching each other. Now
let the lamp be connected
up, and the current will pass
from C, through the electro-magnet,
the mass of the apparatus,
and return by the
wire connecting the lower
carbon-holder with Z. The
carbon points will glow, but
the magnet then attracting
M moves the lever, L, the
piece, Q, engages the wheel
I, pushing it one tooth forward.
But this movement
of the lever establishes a
contact at X, so that the current
abandons the electro-magnet,
to pass the shorter
way, and M being no longer
attracted, the lever is pushed
back by the spring, the contact
at X is broken, and the
magnet being again excited
the lever turns as before, and
Q pushes I round the space
of another tooth. These
alternating actions succeed
each other with great rapidity,
and effect the separation of
the carbons through the train
of wheels acting on the racks.
These movements continue
until, in a second or two,
the separation of the carbons
has become so great, that the
current passing through the
electro-magnet is no longer able to operate against the weight of the upper
carbon-holder, and this happens when an arc of proper size is produced, this
required result being brought about by proper adjustment of the parts of
525the apparatus, marked by the letters R, K and X. But as the carbons are
consumed, the increase of the length of this arc further weakens the
current, until the spring attached to the lever, L, prevails over the
attractive force of the electro-magnet on M, and thus withdraws the catch,
Q, altogether, when the wheels being free to turn, the weight operates to
bring the carbons nearer together, until, with the lessened resistance, the
energy of the current is restored, and Q again comes into play to arrest
the approximating movement. It may be seen, from the above explanation,
that this lamp is automatic; in other words, when it has once been
properly adjusted, it is lighted by merely completing the circuit.
For fixing the carbons properly in their holders there are, of
course, other regulating screws. How very nearly perfection
the automatic regulation of the arc electric lamp has been
brought by such contrivances as these, will be obvious to all
who have noticed the steadiness that has been attained in all
the modern installations.
Fig. 280f.—Jablochkoff Candle.
An ingenious plan was devised by Jablochkoff for dispensing
with all mechanism for regulating the distance of the carbons.
This invention is known as the electric candle, and is of great
interest from the fact that it was with this arrangement that the
electric light was, for the first time, practically employed for
street and theatre illumination. This was in 1878, when visitors
to Paris, during the Exhibition, were astonished by the splendid
displays in the Avenue de l’Opéra, at the shops of the Louvre,
and at some of the theatres. Then it was shown, for the first
time, that electric lighting was not merely a scientific curiosity,
but a new and formidable rival to gas. The Jablochkoff candles
were also subsequently used in the electric lamps on the Thames
Embankment. The principle of the contrivance will be understood
from fig. 280f. Two carbons, C and D, are placed parallel
at a little distance apart, and the space between them is filled
up with plaster of Paris, kaolin, or some similar material,
through which the current will not pass, but which burns, fuses,
volatilises, or crumbles away by the heat produced by the passage
of the current between the two carbons. These carbons
are, of course, fixed in insulated holders, and to start the candle
a small tip of carbon paste is made to connect the carbons at
the top. The Jablochkoff candles must be used with currents
rapidly alternating in direction. The reason for this is, that
otherwise one of the carbons (the positive one) would be consumed
quicker than the other, and that would cause the distance
between them to increase, until it became so great that
the current would cease to pass, and the light would go out. In
order to obtain such alternating currents with the Gramme
machine, a special apparatus had to be devised to change its
direct into alternately reversed currents; but, dynamos intended to supply
electric lights are now made without commutators, and they supply rapidly
succeeding currents in opposite directions. In certain types of dynamos,
again, the armature coils are stationary, and it is the field magnets that
are made to revolve, and in these cases, not even a sliding contact is
required, but the end of the armature coils are directly and permanently
connected with the main circuit. But as these dynamos are self-exciting,
the electricity induced in a few of the armature coils is collected apart
526from the main circuit, and passed through the electro-magnets of the
machine itself, after the alternate currents have, by means of a commutator,
been converted into one direct continuous current.
Fig. 280g.—Electric Lamp.
The arc electric light, as used for the illumination of streets and public
places, is too intense and concentrated to be pleasant to the eye, and
therefore it has been
found necessary to
surround it by globes
of enamelled glass, or
of porcelain, or of
ground glass, or of
frosted glass. By
these expedients for
diffusing and softening
the light, it is
rendered much more
acceptable, but this
advantage is gained
at the cost of a considerable
loss of the
whole illuminating
power, a loss which
is, probably, never
less than 10 per cent.,
but is usually much
greater. The globes
used in Paris, with the
Jablochkoff candles,
were of enamelled
glass, and the apparatus
was arranged, as
shown in Fig. 280g,
where it is partly represented
in section,
and with a part of
the globe broken off,
in order to show one
of the candles placed
in the holder which
connects it with the
circuit. In each lamp
several candles were
mounted, in some
cases four; but the
lamps in the Place de
l’Opéra held twelve.
At first there were
mechanical arrangements,
automatic and otherwise, by which, when the candle was burned
down the current could be turned on to another. But M. Jablochkoff
afterwards discovered that there was really no need for such a mechanism.
For when the whole of the candles are simultaneously and equally
connected with the circuit conductors, it is found that one of them will
527more easily transmit the current than any one of the rest, and when that
particular one has once been lighted by the heat developed, the current
will pass almost entirely through the arc, any loss through the connecting
strip of carbon, at the tops of the other candles, being quite insignificant.
When the first of the candles has burnt down completely, until the insulating
porcelain holder separates the carbons, the current will at once
re-establish itself at the top of one of the remaining carbons, and so on,
while one is left.
The arc electric light has not been brought to its present position
without the expenditure of much care and ingenuity in the preparation of
the carbons used for its production. When Davy first produced the
voltaic arc, the electrodes he used were simply sticks of charcoal. These
were very quickly consumed, and a more durable form of carbon was
sought for. This was found by Foucault, who made use of rods sawn out
of the carbonaceous residue left in the retorts in the process of making
coal-gas. This substance was, however, by no means uniform or
sufficiently pure, and the light obtained was consequently unsteady. Many
experiments were made in preparing special carbons. Pounded coke,
coke and charcoal, were mixed with syrup or tar into a paste, which was
moulded and compressed, and then the sticks were kept in covered vessels
at a high temperature for many hours. Acids were used for purification,
and also alkalis, to remove silica. At the present time there are several
manufacturers of electric light carbons who carry on extensive operations
by processes which probably are very similar one to another, and which
may well be represented by M. Carré’s, whose carbons have the highest
reputation. M. Carré prefers a mixture of powdered coke, calcined lampblack,
and a syrup made of sugar and gum. The whole is well mixed
and incorporated, water being added from time to time to make up for loss
by evaporation, and to give the paste the proper degree of consistence.
The paste is then subjected to compression, by which it is forced through
draw-holes, and the carbons, having been piled up in covered crucibles, are
exposed for a certain time to a high temperature.
As a practical illuminant for lighthouses, the arc electric light came into
use many years ago (1862) as we have already seen. This was when the
generator of the current was the magneto-electro machine; but, now,
when this generator has developed into the modern dynamo, the cost of
the electric supply has been enormously reduced, so that, power for power,
electric lights may be worked at half the former cost, and with greater
convenience and certainty. Light for light, electrical illumination is said
to be far cheaper than gas. Again, the arc electric light has properties
which have caused it to be employed, not only in every important lighthouse
in England, France, Russia, America, and elsewhere, but most ships
of war are provided with means of projecting a beam of electric light in
any direction, in order that the presence of torpedo boats, etc., may be
discovered at night, or harbours entered and signals made under circumstances
when such operations would be otherwise impossible. It was by
the use of the electric light that, in 1886, one of the Peninsular and
Oriental Company’s steamers passed safely through the Suez Canal, at
night, and the experiment was so satisfactory, that the canal authorities
placed beacons and light-buoys to guide such vessels, as, being provided
with electric apparatus, were enabled to hold their proper course between
its banks. The use of projected beams for watching the movements of
enemies, and for signalling to great distances in time of war, has been
528recognized by all the great military powers. The advantage of the
electrical light in some mines, in subterranean and submarine operations
and generally, in work that has to be carried on at night by large bodies
of men, is constantly finding illustration. Few readers are unacquainted
with the brilliant effect of the arc lamps in exhibitions, parks, &c.; at out
of door fêtes, or applied to the illumination of fountains, such as those at
the Paris Exhibition of 1889.
The arc lamps are used in series; that is, where there are a certain
number of lamps to be supplied, the same electrical current circulates
through the whole of them, and this, of course, must have force enough to
overcome the resistance of the whole circuit. Thus, at each lamp, the
intensity of the illumination must necessarily be very great. A solution
was long sought to the problem of so dividing the current energy, that it
might be made to produce lights, of moderate intensity, at a greater
number of points. When Mr. Edison, shortly after having invented the
phonograph, announced that he had solved the problem of the electric
light division, there was a great panic amongst the holders of shares in
gas companies, and a heavy fall in this kind of stock immediately occurred.
As it turned out, the alarm was unnecessary, for gas was not to be superseded,
immediately and definitely, by electricity. Nevertheless, it is by
virtue of the principle that was contained in Edison’s invention, that
electric lighting has assumed the wide-spread importance it has at the
present day, and that it is now actually ousting gas as an illuminant in
the business and domestic premises of our large towns, and in theatres,
libraries, and other places of resort. The principle which has brought
about this great development of electric illumination is that shown in a
simple form in Fig. 261. It appears, however, that as early as 1841, a
platinum wire, made incandescent with a battery current, was proposed as
a source of light, and in 1845, carbon was used in the form of slender rods,
by King, and also by J. W. Starr, in the United States. Both inventors
inclosed their carbons in glass tubes, from which the air was exhausted,
so that the carbon might not burn away. In the following year, Greener
and Staite turned their attention to lamps of this kind, and, again, in
1849, Petrie worked on the same subject. After that, the problem ceased
to engage attention, until, in 1873, a Russian man of science, named
Lodyguine, took the matter up and patented a carbon incandescent lamp,
which did not, however, prove a practical success, and although the idea
was worked out in various ways by Konn, Reynier, Trouvé, and others,
the apparatus they designed was, in every case, lacking in simplicity,
and certainty of action. The Edison incandescent lamp, the announcement
of the discovery of which so fluttered the gas companies, about
1878, was a reversion to the plan of an incandescent metallic wire.
This wire was made of an alloy of platinum and iridium, which was
adopted by Edison on account of the very high temperature required
for its fusion. And in order to prevent the temperature from quite
reaching that point, the wire was arranged in a spiral within which
was a rod of metal that, by its dilatation with a certain temperature,
caused a contact to be made which diverted part of the current
through a shorter circuit, and thus lowered the temperature of the spiral
to within the assigned limits. But the advantages presented by carbon
over metallic conductors led Edison to attempt the formation of filaments
by charring first slips of paper, afterwards slips of bamboo. About the
same time Mr. J. W. Swan, of Newcastle-on-Tyne, was experimenting in
529the same direction, and, in the latter part of the year 1880, he exhibited
the first incandescent lamps shown in England. Swan’s carbon filaments
were prepared from cotton threads which had previously been steeped in
dilute sulphuric acid, washed, and passed through draw holes to give them
an uniform section. They are thus made perfectly homogeneous throughout,
and, after having been wound on pieces of earthenware to the required
shape, they are carbonized by packing in powdered charcoal and heating.
These filaments are very thin, but solid and elastic. The arrangement of
the lamp (see Fig. 280h) is extremely simple: the filament of carbon bent
into a horse-shoe form, or turned so as to form a
loop, is inclosed in a glass bulb of a globular or
egg shape, about two inches in diameter. The
extremities of the filament are connected in an
ingenious manner to two platinum wires that pass
outward through the glass into which they are
fused, and terminate either in binding screws or in
two small loops. The bulb is exhausted first by
an ordinary air-pump, and then by a Sprengel
mercurial pump, the current of electricity being
sent through the filament during the last stages of
the process, and finally the bulb is hermetically
sealed. The light yielded by these lamps is mild
and steady, and its intensity depends on the electric
current sent through them; but this may,
it is said, be carried as high as to make the light equal to that of twenty
candles. Each horse power of force expended on the dynamo suffices to
maintain ten of these lamps. At the Exhibition of Electrical Apparatus
at Paris in 1881, the Swan lamp received the gold medal as being the
best system in its class. The Swan and the Edison patents are now
worked together by one Company, and the productions of this Company
are very largely used, although there are several more or less modified
systems of glow lamps prepared by other manufacturers.
Fig. 280h.
The great advantages offered by electric glow lamps over gas-lights
caused them to be speedily adopted by the most enterprising managers of
theatres and places of amusement. Mr. D’Oyly Carte had the Savoy
Theatre, in London, completely fitted up with these lamps in 1881. The
light was soft and agreeable, it did away with the risks of fire both for the
audience and the performers: for the footlights and scene-lights were
also electric glow lamps, and the coolness of the house and greater purity
of the air were at once appreciated. Several other London theatres have
since adopted the incandescent electric lamps, and it is obvious that the
system will become universal. In all ocean-going passenger steamers,
electric lighting of the saloons and cabins is now the rule. No mode of
illumination so readily adapts itself to the production of artistic and
decorative effects as the glow lamps: for the covering glasses may be
tinted of any required shade, and the lights may be placed in any position.
Small glow lamps are occasionally used as personal adornments, when
placed, for instance, as part of a lady’s head-dress amidst diamonds, a
novel effect of great brilliancy is produced. It need hardly be said that
in this application the wearer is not required to carry a dynamo about
with her, for the electricity is supplied in a manner much more convenient
for this purpose by a device presently to be described. For several years
electric incandescent lamps, supplied by the like means, have been in
530action every night in the carriages of the trains running between London
and Brighton, and more recently the Company have had electric reading
lamps of five candle-power fitted up in the carriages of the main line
trains. They are placed at the backs of the seats just above the passengers’
head. When anyone wishes to make use of one of these lamps, he
places a penny in a slot, and then, on pressing a knob, the light appears,
and at the end of half an hour it is automatically extinguished; but, of
course, it can again be made to appear by another penny dropped in the
slot, and so on every half-hour as long as may be required.
To maintain the electric light (whether arc or incandescent) quite
steady, the greatest uniformity in the speed of the dynamo is essential;
and if the prime mover by which it is worked, whether steam-engine, gas-engine,
water-wheel, or turbine, is not perfectly regular in its action, the
lights will fluctuate in brightness, and thus produce an effect which is
very unpleasant. This is entirely obviated by the adjunct we have now to
describe, which not only is most efficient as a regulator, but is, moreover,
of still more importance by also providing the means of storing up the
electrical energy in a portable form. The reader will have understood
that in a voltaic cell the production of an electric current is the concomitant
of a chemical union of substances within the cell (p. 493). Now, in
the experiment shown in Fig. 263 (p. 498), it is the reverse of combination—namely,
the decomposition of the water that is supposed to be effected
under the influence of the current from a galvanic battery, and the poles
are so connected that the direction of the current in the liquid while the
decomposition is proceeding is from the wire in the O tube to that in the
H tube. If the experiment be interrupted by removing the battery, and
then putting a galvanometer (Fig. 258) in its place, the galvanometer will
immediately indicate a current passing through the apparatus in a direction
the reverse of the former one—that is, in the liquid it goes from H to
O, and the volumes of the gases will slowly diminish while water is reproduced
by imperceptible and gradual re-combination. Batteries can be
made by joining up a series of arrangements like Fig. 263, consisting of
nothing but strips of platinum surrounded by hydrogen and oxygen gases
and the intervening acidified water. Analogous results are obtainable by
cells containing other compounds with suitable metallic poles, for when
decomposition has been effected through a series of such cells by a sufficiently
powerful current from a primary battery, the series of cells will
constitute, on removal of the primary battery, a secondary battery, for
when the terminals of this are joined, the current will flow in the reversed
direction while the separated parts of the original compounds are re-combining
within the cells. These secondary batteries are called also
polarisation batteries. A form of secondary battery was contrived some
years ago (1859) by M. Gaston Planté, in which the current of the primary
battery was made to act on plates of lead immersed in dilute sulphuric
acid. The effect was to coat one of the lead plates of each pair with lead
oxide; and in the action of the secondary battery this was reversed, and
the plates gradually returned to their original condition, when, of course,
the current ceased. Some improvements were made in the Planté battery
by Faure, who coated one of a pair of very thin lead plates at once
with a film of red oxide of lead, and used a layer of felt to separate
it from the other plate. Such arrangements have been called “accumulators”;
another term applied to them is “storage batteries”; but it is
not to be supposed that in them electricity is stored or, so to speak,
531bottled up. They consist merely of such an arrangement of materials as
that when a current (direct, not alternating) from a dynamo is passing,
certain substances are placed in a position of chemical separation in such
a manner that in re-combining an equable current of electricity is produced
in the conductor externally uniting them. We need not notice some
slight modifications of the Faure cells that have been lately introduced,
as no new principle is involved. The light of incandescent lamps worked
by the Faure accumulator is perfectly free from the fluctuations which may
usually be noticed when the lamps are directly connected with the dynamo
only. Even if the engine should stop altogether, the light may be maintained
for hours. The accumulator has also the advantage of giving out
the electric energy that may have been imparted to it days before; so that
when a house is fitted up with an independent electric light installation,
there is no necessity for running the dynamo all the time the lamps are in
use, as two or three days weekly may suffice to charge all the accumulators.
Then there is the portability of the accumulator, which permits
electrical energy to be made use of in situations where dynamos and
prime movers would be impossible. It is said that a large Faure cell
weighing about 140 lbs. can receive and give out energy equal to one
horse power for one hour. In the arrangement for the reading lamps in
railway carriages referred to above, accumulators are placed under the
seats; and it need hardly be said that when the electric light has been
seen in a coiffure, a small Faure cell concealed about the wearer’s person
has supplied the current. A very interesting and useful application of the
accumulator is the portable electric light lamp for miners made by the
Edison-Swan Company. It is simply an incandescent lamp protected by
a strong glass cover attached to the side of a cylindrical case containing
a four-celled accumulator. This lamp is provided with an ingenious contrivance
by which the circuit would be interrupted, if by accident the
outer glass cover of the lamp were broken. Let us now see what another
new development of the applications of electricity gains by the use of accumulators
by turning our attention to the electro-motor.
At the Vienna Exhibition of 1873, the Gramme Company showed two
of their machines, and it is said that when one of these machines was at
rest, a workman connected the ends of two covered copper wires with the
other machine, thinking that these were placed to carry the current from
that machine when in movement. Everybody was surprised when,
without any power from the machinery, the ring was soon in rapid
rotation. These wires were in fact joined up to the other Gramme
machine which was already in action, and it was the current from this that
set the former in motion. There is no reason why this story should not
be perfectly true, although there are good reasons for believing that the
electro-motor was the result of no such accidental circumstance. The
attractions and repulsions between the poles of electro-magnets was soon
seen to supply an available source of motive power, and the subject has
been already mentioned on page 518. Professor Jacobi, of St. Petersburg,
seems to have been the first who constructed an electro-magnetic engine,
the exciting power being the current supplied by a voltaic battery. This
was in 1834, and in a few years afterwards the Professor applied his
engine to a small paddle-wheel boat, 28 feet long, which was electrically
propelled for several days, but at a slow speed. The engine in this case
was virtually a magneto-electric machine worked backwards, that is,
instead of applying power to turn the machine and so produce a current
532of electricity, the current was supplied by the battery and produced
power. In 1850, an electro-motor of five horse power was shown by an
American, Mr. Page, the principle of which may be illustrated by supposing
a reversal of the action represented in Fig. 271, thus: if, instead
of producing currents by moving the magnet, C, in and out of the coil,
A B, we substitute a battery for D, we can, by alternating the direction of
the current through the coil, cause a reciprocating motion of the magnet,
C, and this again may be described as a magneto-electric machine
worked backward. It was soon recognized that no practical electro-motor
was adequate to the production of such high powers as the steam
engine supplies, and that the cost must necessarily many times exceed
that of steam power. But certain advantages, nevertheless, pertained to
the electro-motor in certain positions, as instance in safety, and where a
small force only was occasionally required. Now, when the Gramme
machine was invented to supply currents of electricity under conditions
much more favourable than the magneto-electric machines it superseded,
and at a cost vastly less than that of any voltaic battery, it is highly
improbable that the relation of the new current generator to the production
of electro-motive power would long be overlooked.
The electro-motor may, therefore, be considered simply as a dynamo
worked backward, and almost any form of dynamo may in this way be
used as an electro-motor, that is, a current being supplied either from a
battery or from a dynamo, the motor converts the electrical energy into
mechanical energy. Any dynamo that supplies a direct and continuous
current can thus be used; but there are certain conditions which make it
desirable to somewhat modify the proportions and arrangement of the
several parts when the machine is for motor purposes.
In general, any source of current may be used, but in the applications
of the electro-motor there are chiefly two methods in practice of supplying
the current. The one takes the current from a dynamo in motion, the
other from an accumulator which has previously been “charged” by a
dynamo.
Both of these methods are used in the familiar and interesting application
of the electro-motor to the propulsion of carriages on tramways and
railways. For the latter, indeed, an attempt was made half-a-century ago
on the Edinburgh and Glasgow railway, to employ the force of an electro-magnetic
machine actuated by a battery. This was in 1842, and although
this electric locomotive was fitted up completely, it did not attain a speed
of more than four miles an hour. The weight with the batteries, carriage,
etc., exceeded five tons. But in the recent inventions which have been in
practical operation in many places, it is found quite easy to dispense with
any current producer on the electric locomotive itself, for the electricity is
supplied by a fixed dynamo and the current is transmitted along the line
by a conductor from which a sliding contact conveys it to the electro-motor,
which is attached to the framework of the carriage and acts on the
driving axles of the wheels directly or by toothed gear. In such cases the
return current is carried either by another conductor or by the rails
themselves. In another arrangement one rail conveys the current to the
locomotive and the other returns it. When the rails are so used they
have, of course, to be insulated from the ground and laid with special
electrical contact pieces joining their consecutive lengths, and all the
carriage wheels have to be insulated, so that the currents shall flow only
through the coils of the electro-motor. A railway on this system has
533been worked at Berlin for some time, and a short tramway on the same
plan has lately been opened at Brighton. The Bessborough and Newry
Electric Railway (Ireland) uses a single separate conductor three miles
long, and the power is supplied at a very small cost from a dynamo
station near the middle of the line, where water power is taken advantage
of to drive a large turbine. Quite recently electric propulsion has been
adopted on some of the short tunnel lines in London, and it is quite
probable that ultimately the system will be adopted throughout the whole
course of the underground railways, with the view of obtaining a purer and
more agreeable atmosphere.
Fig. 280i.—Poles with Single Arms for Suburban, Roads.—The Ontario Beach Railway, Rochester, N. Y.
A very light electric railway has been designed, in which the cars run
along rails attached to posts at such a height above the ground as may be
534required to make the line level, or with only slight gradients. The rails
also serve as conductors. This is known as the telepherage system, and
it is found to be well adapted for light loads in an undulating country.
Fig. 280j.—The Glynde Telepherage Line, on the system of the late Fleeming Jenkin.
The other plan which makes use of accumulators commends itself for
application to ordinary tramway carriages, because no conductors are
required along the line, and each car can move independently. The chief
objection is the great weight of the accumulators and the space they
occupy, although they are usually placed under the seats without much
inconvenience. There are at present (January, 1890) six electric tramcars
running in London, and the accumulator system would no doubt have
been applied largely as the motive power for the ordinary street omnibus,
but for the difficulty of controlling them under the momentum of the great
mass of the accumulators, etc. The same objection lies against the use of
the accumulators and motors for propelling tricycles, although such
machines have really been used. But accidents such as occasionally
happen to such vehicles would be attended with additional risks of
injury from the acids of the secondary battery, etc. But there is one
mode of using electric propulsion, that is free from every objection and,
indeed, offers great advantages. Only two years ago the first electric
boat on the Thames was tried experimentally between Richmond and
Henley, and the result was entirely in favour of the electric over the
steam launch. The Faure battery, or so-called “storage cells,” are
arranged beneath the floor of the boat for most of its length in the
smaller boats, and the electro-motor is directly coupled with the screw
shaft. The electric launch has these advantages: perfect safety, freedom
from dirt and smoke, no thumping or vibrating, no noise of steam
discharge, or smell of hot oil, no engineer or stoker is required, and
much larger space available for passengers. One of these electric launches,
not going full speed, is able to travel sixty miles without having the
accumulators recharged. A considerable number of these launches are
already in use, and many more are in course of construction. They are
made of all sizes, from the smallest to those that will carry quite a large
535company, and may be used for excursion parties on the river. The
description of one of these last states that she is 65 feet in length,
and 10 feet across the beam. She can carry sixty passengers, and
twenty can dine in the saloon at one time. There are lavatories, pantries,
dressing rooms, etc., and a brass railed upper deck, with an awning. At
night this boat is lighted up with electric glow-lamps, the current for these
also being supplied by the accumulators. The Electric Launch Company
has stations with Gramme machines at work to charge cells ready to
replace exhausted ones at several places, namely Hampton, Staines,
Maidenhead, Boulter’s Lock, Henley, Reading and Oxford. There is
every prospect of a general extension of the electric propulsion of boats,
and visitors to the Electrical Exhibition at Edinburgh, in 1890, will find
electric launches taking holiday makers as far as Linlithgow. The boats
will be like those on the Thames, fitted with the Immisch motor. Some
electricians are now sanguine enough to believe that even for large
vessels electricity will yet be able to compete with steam in special cases.
The modes of using electric propulsion that we have just noticed furnish
a very interesting chain of conversions of one form of force into another,
with a reversal of the order of transformation at a certain point. Let us
begin with the carbonic acid gas that existed in the atmosphere of the carboniferous
geological period. The solar emanations were absorbed, and
used by the leaves of the plants to separate the two elements of the gas,—the
plant retaining the one in its substance and returning the other to the
air. The plant becomes coal; and ages afterwards the particles of the
two separated elements are ready to re-unite and give out in the form of
heat all the energy that was absorbed by their separation. This heat is
in the steam-engine converted into the energy of mechanical power. This
mechanical power is in the dynamo expended in moving copper wires
through a magnetic field. Every schoolboy who has played with a
common steel magnet—and what boy has not?—knows that the space
immediately round the magnet is the seat of strange attractive and repulsive
force, for he has felt their pulls and pushes on pieces of iron or steel.
This mysterious space is the magnetic field, and although a person would
not be able to perceive that mechanical force is expended when he moves
a single copper ring across such a field, he will readily become conscious
of the fact when he moves a number at once that form a closed circuit;
and he should not omit the opportunity of feeling this for himself if he is
allowed to turn the handle of such a machine as that represented in
Figs. 275 or 277. The mechanical power is absorbed in the dynamo
because the movement induces an electric current that would of itself
produce motion in the machine in the opposite direction. However, the
electricity induced by magnetism and motion is made to pass through the
Faure cell or accumulator, when it does chemical work by separating
oxide of lead from sulphuric acid, leaving these substances in a position
to unite together again, when this action produces a reverse current of
electricity through an external metal circuit. The coils of the electro-motor
form this circuit; the electricity induces magnetism, and the magnetism
gives rise to visible motion and mechanical power.
From what has been already said, it will be obvious that a pair of
covered copper wires connecting a dynamo with an electro-motor
becomes a very convenient means of carrying power from one place to
another. There are situations in which shafts, belts, or any other
mechanical expedients are troublesome or impossible to use for this
536purpose. For instance, a dynamo working at the mouth of a tunnel or
coal-pit may be made to drive any machinery within with nothing between
but the motionless wires. Or a single dynamo will supply moderate
power to a number of small workshops, provided each has an electro-motor,
with no other connection than a pair of copper wires. This
arrangement is found very advantageous for light work and where power
is required occasionally, as in watch-making, the manufacture of philosophical
instruments, etc. Such moderate power is occasionally in
demand also in private houses, to drive sewing machines, lathes, etc.; and
it is obtainable from the same source as the current for lighting. Private
installations for lighting purposes usually have a dynamo driven by a gas
engine, and working into a set of accumulators. It seems not a little
remarkable that if the gas were burnt in the ordinary way instead of being
used in the gas engine, it would give only a fraction of the amount of the
light it causes to be given out by the electric light lamps. But at the
present time, houses and business premises are supplied with electricity
by companies who carry electric mains through the streets. In England
these electric mains, which are thick insulated copper wires, are
inclosed in iron pipes and laid beneath the pavement, like the gas mains.
In the United States, where electric illumination is much used, the
conductors have been usually carried overhead like telegraph wires, but
not a few fatal accidents have occurred from these conductors falling
into the streets. There is no reason to doubt but that in a short time it
will be as common for households to draw upon such electric mains for
their supply of light and power as it now is to draw gas and water from
common mains. The electric supply companies have central stations in
suitable positions, where very large and powerful dynamos are regularly
driven by steam power. These stations are provided with appliances for
measuring the currents and for duly controlling the energy sent out.
What will appear very extraordinary when we remember that electricity
is in itself unknown, is that the quantity supplied to each house or
establishment can be actually measured, and is paid for by meter as in the
case of gas. As already said (page 498) electricity can only be measured
by its effects, and it is the chemical effect which it is found convenient to
use for the purpose we are speaking of. The plan is simply this: two
plates of zinc dip into a solution of sulphate of zinc, and from the one to
the other there is sent through the solution one-thousandth part of the
current to be measured. While the current passes, zinc is deposited on
the plate towards which the current goes in the solution, and if this plate
is periodically weighed this furnishes the measure of the total current.
But how is just one-thousandth of the whole current taken off from the
rest and made to circulate through the measuring apparatus? This is
very easily done by taking advantage of the law of derived circuits, which
for our present purpose may be stated thus: when a current of electricity
finds two different circuits along which it can pass, it will divide and
circulate through both of them, but the greater part will pass through the
circuit of less resistance (if there be any inequality), and by adjusting the
resistances of the circuits we can divide the current between the two
partial or derived circuits in any required proportions. Electric resistances,
it may be mentioned, depend upon the length, section, and nature
of the conductor, and are very easily measured and adjusted.
While the method just explained serves very well to measure the quantity
of electricity that has passed through a conductor in a given period,
537provided that the current has always been in the same direction, it will
be sufficiently obvious that it would fail altogether in the case of alternating
currents. And, in fact, even in the case supposed this mode of
measurement does not take account of the real energy set in motion. A
reference to page 498, where the differences of electric currents are mentioned
that are commonly spoken of—tension and quantity—will show
that electric effects depend upon more than the quantity of electricity
passing. Forms of apparatus have been devised for recording the total
energy supplied; but their construction and principles are too complex
to be here explained. In some cases high tension currents are required,
in others it is quantity and not tension that is sought for; and there are
ways of transforming the qualities of currents so that the same source
shall supply electricity of either class. An example of this may have been
noticed in the action of the Ruhmkorff coil, where the mere interruption
of the primary or battery circuit, which possesses so little tension that of
itself it could not give rise to a spark, nevertheless produces a wave of
electricity in the secondary circuit of a tension so high that sparks several
feet long may be produced by it.
A somewhat recent application of the electric current of the dynamo
may be just mentioned here. It is what is known as electrical welding,
and depends upon the heat developed by currents being proportioned to
the electrical resistance for each part of the circuit. The heat thus generated,
where the current passes between two surfaces of metal, even of
considerable dimensions, is sufficient to bring them to a semi-fluid condition,
so that when simply pressed together they coalesce into one mass.
In this way pieces of iron work can be welded together in situations where
it would be either inconvenient or impossible to heat them by furnaces.
The reader who has followed the last article will probably be prepared
to admit that “the magnetic field” is one of the most wonderful things in
the whole realm of inorganic nature, as all the powerful effects we have
been describing are the results of merely moving wires through it. A wire
conveying an electrical current so modifies the space surrounding it, or
so acts upon the unknown pervading medium, that conductors moved in
it, have other currents generated in them. An intermittent current, like
that in the primary circuit of the induction coil, is equivalent to a movement
of the magnetic field in regard to the secondary coil, so that the
general principle in the coil and the dynamo is fundamentally the same.
Quite recently, Professor Elihu Thomson has shown some very novel
mechanical effects of repulsions and rotations of conductors placed near
the poles of a coil through which rapidly alternating currents are passing.
[1890.]
We already hear of natural forces which have hitherto in a manner run
to waste being now utilised in man’s service by the advantage taken of the
capability of a slender wire to convey power. A notable instance is in
the case of the famous Falls of Niagara. Here the head of water is used
to drive turbines; our readers must not run away with any notion of huge
water-wheels being placed below the falls. But from the high level of
the water above the falls a tunnel has been cut which brings the water
into pipes 7½ feet in diameter, and these deliver it into three turbines, in
passing through which it develops a force of 5,000 horse power, and this
force is communicated to a steel shaft 2½ feet in diameter, connected with
the revolving parts of the dynamo. Mr. G. Forbes, the engineer, states
that the company who have undertaken this enterprise are supplying,
538with a handsome profit to themselves, electrical current or power at ⅛th
of a penny per unit, for which English companies charge sixpence.
That is, Niagara supplies power at 1 48th of the price it can be obtained
from coal.
The fact that mechanical power can be brought from a distance to
everyone’s door by a slender wire, and at small cost, suggests the possibility
of great social and industrial changes being effected in the future by
that one condition. Think of the abolition of factory chimneys and smoke,
nay, even of the abolition of the factory system itself, for cheap power
transmission seems to promise much in that direction, and there is a
shadowing forth of still more in
The Leyden jar and a few of its most obvious and common effects have
been touched upon already, (page 490); but the phenomena which
are revealed by a careful study of its charge and discharge show that
these are by no means of the simple kind that has generally been supposed.
Thus, for instance, if the magnetising effects of what is called
current electricity be borne in mind, especially the definiteness of this
action as regards the direction of the current (cf. Fig. 257), it would follow
that if instead of the iron bar in Fig. 265 we place within the coil some
unmagnetised steel needles we should find after passing a current or discharge
that these have become converted into permanent magnets, and
that their north poles are always towards the left of the supposed current.
Years ago experiments were made to ascertain whether the discharges of
a Leyden jar repeatedly passed through a coil would magnetise needles
in the same way, because it had been assumed that the discharge is simply
a current of extremely short duration and of quite definite direction. As
far back as 1824 it had, however, been observed that the needles were
magnetised sometimes in the wrong direction, yet no attempt was made
to explain this—it was sometimes merely mentioned in the books as
“anomalous magnetisation.” Dr. Henry of Washington, U.S.A., experimented
on the subject, and in 1842 referred this action to a condition
of the discharge which had never before been suggested. He says “we
must admit the existence of a principal discharge in one direction, and then
several reflex actions backward and forward, each more feeble than the
preceding, until the equilibrium is obtained.” Some five years afterwards
Helmholtz had independently arrived at the same conclusion, and from
the fact that when a succession of Leyden jar discharges are sent through
the voltameter (Fig. 263) the water is indeed decomposed, but both oxygen
and hydrogen are evolved at each electrode. Sir William Thomson (now
Lord Kelvin) examined the question from a theoretical point of view, and
in a masterly mathematical paper published by him in 1853 not only showed
that the discharge must be of an oscillating character, but gave the form
of equation by which the rate of oscillation is determined.
Faraday proved, as has already been stated, that the matter of the
dielectric takes part in such condensing actions as that of the Leyden jar.
539The electrical charge enters into the glass, the particles of which are thrown
into a certain state of strain or tension (which Faraday called polarisation),
and the discharge of the jar is their release from that tension. So that it
appears that whatever electricity may be, it can in some way become
bound up with the particles of ordinary matter like glass and other dielectrics,
and exert force upon them, which force acts always in two
opposite directions. It is the opposition of the form or direction in which
the electrical effect is manifested that gave rise to the conception of the
two “fluids”—the “positive” and the “negative.” If these “fluids”
really existed it would surely have been possible to give to an insulated
body an absolute charge of either of them. But this can never be done;
if, for instance, you have in the middle of a room a metallic sphere charged
with positive electricity, the necessary condition is that on the walls of the
apartment or on surrounding objects there is an exactly equivalent quantity
or negative electricity.
The number of oscillations or alternate momentary currents in a single
discharge of a Leyden jar is enormous. Theory shows that under ordinary
circumstances they must be enumerated by hundreds of thousands, if not
by millions; that is, the apparently instantaneous spark is really made up
of say a million surgings to and fro of the electric influence. But theory
also shows that the frequency of these oscillations can be controlled or
adjusted through an indefinite range. A general notion of the requisite
conditions may be obtained by the analogy of sound, and for this we may
take the familiar case of the strings of a musical instrument, say the violin,
or the harp. Everybody knows that when a stretched string or wire is
pulled a little aside it is in a state of lateral strain, striving by its elastic
force to return to its position of rest, and if it is suddenly let go it not only
rapidly regains that position, but by the inertia of its motion is carried
beyond it against its elastic force, which, however, again brings it back,
and the movement is continued nearly up to the point at which it was
originally released, this swinging movement persisting for an indefinite
period, during which the vibrations, which have an ascertainable and perfectly
regular frequency, are communicated to the sounding-board of the
instrument and from that to the air, by which they are conveyed to the ear
and affect the auditor as a musical note, which note is higher as the number
of vibrations per second is greater. Everybody will have observed that in
the violin the note yielded by each open string is higher as the tension
becomes greater by turning the peg to tighten it; that the same string
will, without any change in its tension, yield higher notes as shorter lengths
of it are employed. Another circumstance upon which the pitch of the
note depends may also be illustrated in the violin, in which it will be noted
that the G string, which gives the lowest notes, is loaded with wire wound
spirally round it. Here, then, are three circumstances that collectively
determine the pitch or number of vibrations of a string—tension, length,
weight; and if you give the measures of these to a mathematician he can
tell you the note the string will emit, for the number of vibrations is given
(when the measures are expressed in the proper units) by the formula
√t
n =
2l√w
This shows that we have only to adjust suitably the tension, length, and
weight of a string in order to make it vibrate at any rate we please. Now
in the oscillation of currents in the Leyden jar discharge there are conditions
540which correspond, by analogy at least, with those that determine the
vibrations of a stretched string. These conditions are of course electrical,
and they are definable in terms of electric units, which need not be discussed
here. As we are leading the reader to the modern view of electricity,
which sets aside the fluid theories and regards electricity as having no
separate existence, but as being merely the manifestation of some condition
of a universally pervading medium, the same, in fact, as the luminiferous
ether, it is curious to remark that these electrical oscillations would
seem to attribute to the incompressible and imponderable ether something
very much like the characteristic property of matter we call inertia, by
virtue of which the released cord flies past its position of equilibrium to
the other side. Or may this quality be dependent on the matter of the
dielectric in which the ether is, as it were, entangled?
The oscillatory character of the Leyden jar discharge was elegantly demonstrated
before a large audience in a lecture given by Professor O.
Lodge at the Royal Institution a few years ago. Clearly it is impossible
to render perceptible to the senses the millions of periodic discharges that
take place in the marvellously short space of time taken up by a spark,
but by doing what is analogous to slackening the tension of the stretched
string or increasing its length, that is by increasing the static capacity,
which means using a large number of jars combined into a battery, and at
the same time causing the discharge to pass through coils (the effect of
these is to increase the self-induction of the circuit—called also impedance),
an arrangement corresponding with loading the string, Dr. Lodge was
able to bring down the rate of oscillation to 5,000 per second, when, instead
of the crack of the ordinary discharge, a very shrill continuous sound
was heard. The addition of another coil gave another load, and when the
rate was thus reduced to about 500, the note emitted was that of the C
above the middle A of the piano. With the rate of oscillation thus reduced,
it became easy to render the discontinuity of the discharge visible by means
of revolving mirrors, as in the well-known acoustical demonstrations.
Fig. 280k.
Professor Lodge has devised an experiment which again shows the
analogy of electrical oscillations with those by which sound is produced.
It is well known that a vibrating tuning-fork will set another fork of the
same pitch to vibrate also by mere approximation. A and B (Fig. 280k) are
two exactly similar Leyden jars, the inner and outer coatings of each being
connected by a wire enclosing a considerable area in its circuit, which in
the case of A contains an air gap across which sparks pass when the
coatings are connected with the poles of an electrical machine. The
circuit of B is provided with an adjustable sliding piece C, and the coatings
are almost connected with each other by a strip of tinfoil hanging
over the rim but not quite reaching to the outer coating. When the jars
are placed so that their wire circuits are parallel, and sparks are passing
541across the air interval of A’s circuit, a position of the slider on the other
can be found when sparks also pass between the tin-foil and the outer coating.
But if the slider be moved from this position, the two circuits will
no longer be in unison, and the sparks in B will cease. This response of
the oscillations in one jar to those set up in another of the same vibratory
period is called electrical resonance.
Dr. Hertz, a professor in the University of Bonn, has opened out new
paths to investigators by a brilliant series of researches which have shown
that in the dielectric surrounding an electrical system executing very rapid
oscillations there are waves of electro-motive and magnetic force. These
researches are not capable of any condensed description here, and the
reasoning is of a kind that appears mainly to the expert physicist. One
of his modes of investigation required oscillations of extreme rapidity, and
he obtained them by attaching to each pole of an induction coil a metal
plate, and between these plates, which were in the same vertical plane,
passed a stout wire interrupted by an air gap in its centre provided with
small brass balls. The rate of oscillation of this arrangement was calculated
as the hundred-millionth part of 1·4 second. In conjunction with
this system Hertz made use of a very simple apparatus he called a resonator,
which consisted merely of a piece of copper wire bent into a circle
of about 28 inches diameter. The ends of the wire did not, however, meet,
but were fitted with two balls, or with a ball and a point, and an arrangement
by which the air gap between them could be very finely adjusted
and measured. This resonator was, of course, prepared as to be in electrical
tune with the original vibrator, and with it Hertz was able to examine the
condition of the surrounding space. When held in the hand near the
vibrator he found that sparks crossed the air space in the resonator, and
that the length of the air space across which the sparks would pass varied
with the position of the resonator. When the plane of the resonator was
parallel with the metal planes of the vibrator and its axis in the horizontal
line drawn perpendicularly through the vibrator’s air space, the sparks
passed readily when the air space of the resonator was at the same time
vertically above or below its centre, but they ceased entirely when it was
level with the centre. He obtained these sparks when the resonator
was held—in free space, be it understood—in the above-mentioned position
even at a distance from the vibrator of 13 yds., the length of the apartment.
By examining the results with other positions of his resonator and
by other and varied experiments, Hertz was able to prove the existence of
definite waves of electro-magnetic and electro-motive forces, to measure
their lengths, and to show that they are capable of reflection, refraction,
and even polarization by the same laws that hold with the extremely
short but enormously rapid vibrations constituting light. It may here
be mentioned that the existence of currents in the resonator can be
shown by a Geissler tube being made to take the place of the air space,
which tube is thus lighted up without any metallic or visible connection
with any electrical apparatus whatever, the only requisite conditions being
that its circuit be tuned to the vibrator, and in a certain position in
relation to the axis of the spark space of the latter. Hertz has also shown
that electro-magnetic disturbances (transversal waves) are propagated in
space with a determinate velocity akin to that of light, and in short the
outcome of his investigations, as well as of those undertaken by others, has
been a vindication of Clerk Maxwell’s splendid theory by which light is
regarded as an electro-magnetic action. Professor Righi of Bologna,
542having succeeded in obtaining shorter electrical waves than anyone before—namely,
4 10ths of an inch instead of about 20 inches—was able with
them to repeat all the phenomena of optics such as reflection, refraction,
circular polarization, interference, &c. It appears then almost certain
that light and electro-magnetic waves or radiations are but one and the
same affection of a pervading medium we call the ether.
By following up in certain directions lines of research suggested by the
investigations of Maxwell, Lodge, Hertz and others, and by an unreserved
acceptance of the ether theory of light, electricity and magnetism, some
wonderful practical results have recently been obtained by M. Nikola
Tesla, an electrical engineer now resident in New York. The experiments
shown by Tesla in his public lectures have excited great interest in
scientific circles, and have by many persons been witnessed with something
like astonishment.
Fig. 280l.—The Tesla Oscillator.
Fig. 280m.—M. Nikola Tesla.
One of the first objects of M. Tesla was to obtain alternating currents
of high tension and great frequency. It may be seen from Fig. 272 that
the movement of coils of wire in a magnetic field generates currents, and
it has been stated that these currents are in alternately opposite directions
as the coils approach or recede from the magnetic poles. In the machine
represented in Fig. 280a, each revolution would produce 16 reversals of
current. Tesla constructed a rotatory machine which gave 20,000 alternations
of current in one second, because it had 400 poles and could be
rotated at a very high speed. But of course the number of poles and the
speed of the machine could not be increased beyond certain practical
limits. By a happy application of the known principle of harmonic
oscillations, in which all the rotatory movements of fly-wheels, coils and
poles could be dispensed with, Tesla simplified the alternate current
generator, reducing the moving parts to the minimum at the same time
that he obtained a greater number of alternations and almost perfect
regularity in their periodicity. The way in which this has been accomplished
may be gathered from a careful inspection of Fig. 280l compared
with the following explanation. This illustration, it should be
understood, is merely a diagram in which details of mechanism are
altogether omitted, and only so much shown as will serve to explain the
principle. We shall take the mechanical part first, and direct the reader’s
attention to the means by which an iron rod is made to perform very
rapid to-and-fro movements in the direction of its length, and to do that
544with perfectly isochronous periods, which may be made longer or shorter
at will, and which are quite independent of very considerable variations
in the motive power. The diagram represents the apparatus in
section, and the central part of it marked by letters P and P´ is a piston
through which passes what may be called a piston-rod A, which projects
some distance out of the cylinder at both ends. The piston is shown in
the diagram in its central position, where the impelling power has no
action to move it as will presently be seen. This moving power we may
assume to be the compressed air applied through the ports I I´. Just to the
right of the upper one of these on the diagram will be observed in the
piston a slot S opening into a hollow T, which communicates directly with
the space on the left of the piston. The same arrangement, with directions
reversed, is seen on the other side of the piston. If now the piston were
pushed a little to the left of the position shown in the diagram, the compressed
air rushing from I through the slot into the opening S T would
impel the piston towards the right, and it would be carried onward by its
inertia beyond the position shown in the figure towards the right, but in
doing this the access of the compressed air on the left would be cut off, and
the slot communicating with the space on the right hand would allow the
compressed air to act in the space P, checking the further advance of
the piston to the right, acting like a spring or elastic cushion, and again
driving the piston to the left, during which movement the air that has
done its work is allowed to escape at the outlet O O. The same cycle of
operations will be rapidly repeated, but the rate of oscillation admits of
control, for the larger the air chamber in which the air is compressed by
the momentum of the piston and rod, the less will it be compressed and
the less powerfully it will resist, while with a smaller capacity of air-chamber
the more powerful will be the back spring of the imprisoned
air. On the other hand, the mass that is moved may be increased; that
is the weight of the rod, &c., may be increased. In any case the oscillations
will be perfectly regular, because the force which tends to bring the piston
to its position of equilibrium will be always proportionate to its distance
from that point. So that we have here a rod shooting in and out shuttle-wise
with the utmost regularity and with almost any desired rapidity,
controllable under precisely the like conditions as the stretched string
already mentioned, for as the tension of the string is the measure of the
force with which it strives to regain its position of equilibrium, so the
compression of air in the chamber behind the piston; and as the loaded
string vibrates slower, so will the loaded piston. So much for the
mechanical part of this machine, for we may omit all details of valves, &c.
The electrical arrangement is very simple and of the greatest efficiency.
On each projecting end of the piston are wound coils of insulated copper
wire, which being shot in and out across a powerful magnetic field
between the jaws of very large electro-magnets M M´ cut the “lines of
force” to the best advantage, and from these coils alternating currents of
high tension and frequency are gathered up. The vibrating rod is steadied
by working in bearings (not shown). The electro-magnets are actuated
as usual by coils of insulated wire surrounding their iron cores. In the
motion of the moving coils there are electrical forces called into play
which in mechanical effect control the movement in the same way as
the air-springs, and as these electrical forces admit of certain adjustments
and have calculable effects, the mechanical period of the machine
and the electrical one can be made to accord, and thus to, as it were,
545sustain each other, and assure a perfectly isochronous periodicity, even
with considerable variations of the impelling force. Though we have
supposed compressed air as the actuating agent, steam has been applied
in some slightly modified forms of the machine, and sometimes at the high
pressure of 350 lbs. per square inch. Such is Tesla’s alternating current
producer, or the Tesla Oscillator, as it has been called. This, of course,
is a very different thing from the vibrator of disruptive discharge already
mentioned in connection with the experiments of Professor Hertz. Tesla
also uses the disruptive discharge, and what with the high frequency and
the great tension of his currents, he obtains electric oscillations of hitherto
unequalled rapidity, calculable at thousands of millions per second.
He claims, indeed, to be able to agitate the ether at rates of undulation
comparable with those of light itself (500 billions per second). Some of
the experiments he has shown certainly lend support to such an explanation.
The lighting of electric lamps with but one metallic connection,
and that held in a person’s hand, and causing Geissler tubes to light up
without any metallic connections whatever, and making gas at ordinary
pressures luminous, a lump of charcoal contained in a closed glass vessel
to become red-hot while the vessel is merely held in the hand, are certainly
phenomena that cannot be explained on the old lines. The space between
two large surfaces of metal 15 feet apart, and forming the poles of
an oscillatory system, is shown to be full of light-forming influences, as
when phosphorescent substances contained in closed glass vessels glow
intensely, the glass being apparently no obstacle. According to Tesla,
you make space and matter equally permeable to ethereal undulations
when these are tuned, so to speak, to the proper frequency.
Many of the strange effects Tesla has shown are referable to the
principle of electric resonance; such are the powers of a coil with no
metallic connections with any other apparatus and removed, by a distance
of many feet, from any current-conveying wires. Tesla’s workshop was
an apartment 40 feet long and 20 wide, and the wires connecting the
poles of his oscillator were carried round the walls, while in the centre
of the workshop stood a very large but entirely insulated coil, between
the terminals of which an ordinary incandescent lamp was placed. This
lamp was brilliantly illuminated when the oscillator was in action.
The electric qualities of this coil were so adjusted that its currents
came into tune with the ethereal vibrations propagated from the conductor
round the room. But further, a single hoop of copper wire of
the proper diameter and thickness could be brought into unison with the
coil, and when held in the hand over the latter, even at a considerable
distance, incandescent lamps attached to it were lighted up by the induced
currents. Many other novel experiments have been shown by M.
Tesla, but they need not here be described, as they have yet to be
connected with the logical study of the entire class of phenomena. M.
Tesla speaks somewhat sanguinely of being ultimately able to convey
signals, and even power, to a distance, not merely with one wire but
with no wires at all! Another thing he looks forward to is to set the
electricity, or rather the ether that interpenetrates the matter of the whole
earth, into a state of agitation. This seems what is commercially termed
“a large order;” but we have seen that every Leyden jar, every coil,
and in fact every electrical system, has its own period, and if by any
possibility we could discover, or by chance hit upon the earth’s electric
vibration period, it is not antecedently impossible that even the comparatively
546small efforts of such oscillatory vibrations as we could produce,
would by their accumulation agitate the earth’s ether. It is well known
that very small impulses, so tuned as to correspond with the natural
period of a considerable mass, will produce striking mechanical effects.
Thus, a troop of soldiers passing over a bridge have often been known
to break down a structure that would have supported their mere weight
many times over, because they were all marching together and with a
step corresponding in time with the oscillatory period of the bridge. It
is now always enjoined in the military orders that troops in crossing a
bridge must “break step.” Another familiar illustration of the accumulation
of small synchronous impulses is the experiment of singing into a
glass goblet the note corresponding with its vibration period. The singer
merely by sustaining this note for a short time often succeeds in shivering
the glass into fragments. M. Tesla believes that he has already succeeded
in agitating the earth’s ether to some extent; he does at least obtain
flaming purple streamers passing into the air from one end of a coil, while
the other is connected with the earth.
These discoveries and theories appear likely to lead to many unforeseen
results, valuable for both science and its applications, and such as may
far surpass the expectations of those who take less enthusiastic views of
the matter than M. Tesla and his friends do. The theoretical properties
of the ether and the conditions of it, which are held capable of making it
the scene and the medium of all the hitherto so-called ponderable and
imponderable forces, have not been completely worked out. The experiments
that have been already made show that disturbances of very
different kinds may be propagated in the ether by undulations of any
length from less than 1 60000th part of an inch, as in the case of violet
light already spoken of, to the 1,200 miles attributed to certain electrical
conditions.
The foregoing sentences, describing the discoveries of Hertz and others,
had not long been penned before it had become possible to announce that
they had borne fruit in as extraordinary an invention as could have distinguished
the close of an extraordinary century. It is the realization
of what the most accomplished electrician would not long before have
pronounced a dream—namely, wireless telegraphy. The general principle
of it should not be obscure after the account of the “Hertzian
waves”; but our space does not permit a description of details of its
working out in a practical form by a young Italian electrician, Signor
Marconi. We have already seen that a Geissler tube, when its circuit
is properly attuned, can be lighted up by the magneto-electric disturbance
propagated without material contacts, and this itself would constitute a
method of signalling to a distance. On the same principle, a discharge
may be determined by the “wave” between conductors in certain adjustable
conditions of electric tension, and in this way local circuits may be
brought into play, and ordinary telegraphic effects produced, as described
in the following article. The actual apparatus to receive the ethereal
impulses is extremely simple—merely a little fine metallic dust (nickel and
silver) in a glass tube included in the resonator circuit by a wire at each
end, touching the dust. This gathers together, or coheres (hence the
apparatus is called the coherer), under the magneto-electric influence, a
local battery discharge then passes, completing a circuit, and the dust has
to be shaken loose again by a mechanical agitation. Marconi has been
able to signal over a distance of forty-three miles.
547
Fig. 281.—Portrait of Professor Morse.
THE ELECTRIC TELEGRAPH. — TELEGRAPHIC INSTRUMENTS. — TELEGRAPHIC LINES. — THE TELEPHONE.
More than two centuries ago a learned Italian Jesuit, named Strada,
gave a fanciful account of a method by which he supposed two
persons might communicate with each other, however far they might be
separated. He conceived two needles magnetized by a loadstone of such
virtue, that the needles balanced on separate pivots ever afterwards pointed
in parallel directions; and if one were turned to any point, the other also
sympathetically moved in complete accordance with it. The happy possessors
of these sympathetic needles, each having his needle mounted on
a dial marked with the same letters and words similarly inscribed, would
be able to communicate their thoughts to each other at preconcerted hours,
by movements and pauses of the wonderful needles. The poet Akenside,
when describing, in his “Pleasures of the Imagination,” the effect of association
in bringing ideas before our minds, illustrates his point by a happy
allusion to Strada’s conceit. Here is the passage:
548“For when the different images of things,
By chance combined, have struck the attentive soul
With deeper impulse, or, connected long,
Have drawn her frequent eye; howe’er distinct
The external scenes, yet oft the ideas gain
From that conjunction an eternal tie
And sympathy unbroken. Let the mind
Recall one partner of the various league—
Immediate, lo! the firm confederates rise.
‘Twas thus, if ancient fame the truth unfold,
Two faithful needles, from the informing touch
Of the same parent stone, together drew
Its mystic virtue, and at first conspired
With fatal impulse quivering to the pole.
Then—though disjoined by kingdoms, though the main
Rolled its broad surge betwixt, and different stars
Beheld their wakeful motions—yet preserved
The former friendship, and remembered still
The alliance of their birth. Whate’er the line
Which one possessed, nor pause nor quiet knew
The sure associate, ere, with trembling speed,
He found its path, and fixed unerring there.”
In our own day this fancy of Strada’s has been literally and completely
realized in all save the convenient portability of the sympathetic dials; but
this and the other forms of apparatus which are now so familiar in electric
telegraphy were produced by no sudden inspiration occurring to a single
individual. Great inventions are ever the outcome not of the labours of
one but of a hundred minds, and the progress of the electric telegraph
might be traced, step by step, from the first suggestions, made more than
a century ago, of employing, for the communication of intelligence at a
distance, the imperfect electric means then known. The men who then
attempted to utilize the mysterious agency of electricity failed to produce
a practical telegraph, because the conditions of electrical excitation known
at that time gave no scope for the realization of their project. Not the less
do they deserve our grateful remembrance for the faith and energy with
which they strove to overcome the difficulties of their task. Voltaic electricity
was first proposed as the means of conveying signals to a distance
in 1808, immediately after the discovery of the power of the pile to decompose
water; and the method of communicating the signals was based upon
this property. Sömmering proposed to arrange thirty-five pairs of electrodes,
formed by gold pins passed through the bottom of a glass vessel
containing acidulated water. Each pair of pins was marked by a letter of
the alphabet or a numeral, and attached to distinct wires, which could be
put into connection with a pile at the sending station. The signals were
made by the gas evolved from these electrodes indicating the letter intended.
The number of wires required and the slowness of working were
great objections, and this system never came into practical use, although
it was afterwards proposed to diminish the number of the wires from thirty-five
to two—by so varying the amounts of gas given off and the periods of
time as to form an intelligible system of signals. Ten or twelve years after,
Mr. Ronalds, of Hammersmith, invented an ingenious system by which
letters on a dial could be pointed out at a distance by frictional electricity.
Two dials, on which the letters, &c., were marked, were each placed behind
a screen having an aperture, which permitted only one letter to be
seen at once; and the dial was mounted on the seconds arbor of a clock
with a dead-beat escapement. A pair of pith balls hung in front, insulated
and connected by means of an insulated wire with the similar pair at the
other end of the line, where the other clock and dial were placed. The
549clocks were regulated to go as nearly as possible at the same rate, so that
at each end of the line the same letters were simultaneously displayed. It
was easy, however, at any time to start the clocks together at the same
letter by a signal previously agreed upon, and all that was really required
was a synchronous motion of the discs during the time the signals were
being sent. The insulated wire received from a small electrical machine
a charge, which caused the pith balls at both ends to diverge; and the
moment the wire was discharged, the balls collapsed suddenly and simultaneously,
and this discharge was effected by the sender of the message at
the instant that the letter he wished to indicate appeared at the opening in
front of his dial. Since the same letter was at the same instant visible at
the other end also, it was indicated to the receiver of the message by the
collapse of the pith balls. Ronalds worked this telegraph experimentally
with a wire 525 ft. long, but it was never adopted practically. On communicating
to the Admiralty the power of his invention, he was informed
that “telegraphs of any kind were wholly unnecessary, and no other than
the one in use would be adopted.”
The memorable discovery of electro-magnetism by Œrsted in 1819 was
soon followed by attempts to apply it to the production of signals at a
distance. Ampère first pointed out the possibility of making an electric
telegraph with needles surrounded by wires; but he proposed to have a
separate needle and wire for each signal to be transmitted. If Ampère had
but thought of producing signals by different combinations of two movements,
as Schweigger had before suggested for Sömmering’s telegraph,
thus making two wires and two needles suffice, the practical introduction of
the electric telegraph would have dated some twenty years earlier than it
actually did. In 1835 Baron Schilling exhibited an electric telegraph with
five magnetic needles, and he afterwards improved upon it so far as to reduce
the number of needles and conductors to one—for to him the happy
thought seems first to have occurred that one needle could be made to
produce many signals by different combinations of its movements—sometimes
to the right, sometimes to the left. Thus two movements to the left
might stand for A, three for B, four for C, one to left followed by one to left
for D, and so on. Schilling’s apparatus does not appear to have had the
requisite qualities for practical working on the large scale. From this time,
however, telegraphic inventions succeeded each other rapidly, and we meet
with the names of Gauss, Weber, Steinheil, and others, as inventors and
discoverers in the region of practical science which was now fairly opened,
The first two used the magneto-electric machine to give motion to the
needle; and the thought of using the metals of the railway line as conductors
having occurred to Gauss, he found, on making the attempt, that
the insulation was imperfect, but he perceived that the great apparent conductibility
of the earth would allow of its being substituted for one of
the metallic communicators.
But the first who succeeded, after long and persevering effort, in giving
a practical character to the electric telegraph, was undoubtedly Professor
Wheatstone. He had for some years been engaged in electrical researches
before, in 1837–-a memorable year for telegraphic inventions—he took out
a patent in conjunction with Mr. W. Fothergill Cooke. In their telegraph
there were five magnetic needles, arranged in a horizontal row, each needle
being in a vertical position, and the various letters of the alphabet were
indicated by the convergence of the needles towards the point at which
the letter was marked on the dial. The first electric telegraph constructed
550in England was made on this system on the London and Blackwall Railway.
In 1838, Messrs. Wheatstone and Cooke had reduced the number
of needles to two, and many other improvements were effected in the apparatus
for signalling, it being made possible for any number of intermediate
stations to receive the messages. Several great railway companies erected
lines with five lines of wire, but the expense of so many conductors was
found to be considerable, and Messrs. Cooke and Wheatstone, after reducing
the number of needles and conductors to two, ultimately (1845)
patented an instrument with a single needle. It was about this time that
an incident occurred which strongly drew the attention of the general public
to the electric telegraph, which had, up to that time, been considered as
the more immediate concern of the railway companies. A foul crime had
been committed at Salthill, by the murder of a woman named Hart; and
Tawell, the suspected murderer, was traced to Slough station, and there it
was found he had taken the train to London; a description of his person was
telegraphed, with instructions to the police to watch his movements on his
arrival at Paddington. He was accordingly followed, apprehended, tried,
convicted, and executed. This incident has been graphically and circumstantially
described by Sir Francis B. Head, in connection with an anecdote
recording a curiously expressed recognition of the value of the telegraph
in furthering the ends of justice. We give the passage in full:
“Whatever may have been his fears, his hopes, his fancies, or his
thoughts, there suddenly flashed along the wires of the electric telegraph,
which were stretched close beside him, the following words: ‘A murder
has just been committed at Salthill, and the suspected murderer was seen
to take a first-class ticket for London by the train which left Slough at
7·42 p.m. He is in the garb of a Quaker, with a brown great-coat on,
which reaches nearly down to his feet. He is in the last compartment of
the second first-class carriage.’ And yet, fast as these words flew like
lightning past him, the information they contained, with all its details, as
well as every secret thought that had preceded them, had already consecutively
flown millions of times faster; indeed, at the very instant that,
within the walls of the little cottage at Slough, there had been uttered that
dreadful scream, it had simultaneously reached the judgment-seat of
Heaven! On arriving at the Paddington Station, after mingling for some
moments with the crowd, he got into an omnibus, and as it rumbled along
he probably felt that his identity was every minute becoming confounded
and confused by the exchange of fellow-passengers for strangers, that was
constantly taking place. But all the time he was thinking, the cad of the
omnibus—a policeman in disguise—knew that he held his victim like a
rat in a cage. Without, however, apparently taking the slightest notice of
him, he took one sixpence, gave change for a shilling, handed out this
lady, stuffed in that one, until, arriving at the Bank, the guilty man, stooping
as he walked towards the carriage door, descended the steps, paid his
fare, crossed over to the Duke of Wellington’s statue, where, pausing for a
few moments, anxiously to gaze around him, he proceeded to the Jerusalem
Coffee-house, thence over London Bridge to the Leopard Coffee-house in
the Borough, and, finally, to a lodging-house in Scott’s Yard, Cannon
Street. He probably fancied that, by making so many turns and doubles,
he had not only effectually puzzled all pursuit, but that his appearance at
so many coffee-houses would assist him, if necessary, in proving an alibi;
but, whatever may have been his motives or his thoughts, he had scarcely
entered the lodging when the policeman—who, like a wolf, had followed
551him every step of the way—opening his door, very calmly said to him—the
words, no doubt, were infinitely more appalling to him even than the
scream that had been haunting him—‘Haven’t you just come from
Slough?’ The monosyllable, ‘No,’ confusedly uttered in reply, substantiated
his guilt. The policeman made him his prisoner; he was thrown
into jail, tried, found guilty of wilful murder, and hanged. A few months
afterwards, we happened to be travelling by rail from Paddington to Slough,
in a carriage filled with people all strangers to one another. Like English
travellers, they were mute. For nearly fifteen miles no one had uttered a
single word, until a short-bodied, short-necked, short-nosed, exceedingly
respectable-looking man in the corner, fixing his eyes on the apparently
fleeting posts and rails of the electric telegraph, significantly nodded to us
as he muttered aloud, ‘Them’s the cords that hung John Tawell!’”
So far we have followed Wheatstone and Cooke, because these gentlemen
were the first who in any country made the electric telegraph a
success on the great scale. Elsewhere than in England, laboratories and
observatories had been connected by experimental lines, and models
had been exhibited to Emperors, but these two Englishmen were the first
to construct a telegraph for practical use. It must not, however, be supposed
that they are entitled to be considered the exclusive inventors of the
electric telegraph, for we have already named other distinguished investigators
who contributed their share to this remarkable invention. And
some years before Wheatstone and Cooke had patented their first needle
telegraph, the first ideas of a system which has largely superseded the
needles for ordinary telegraphic purposes, had presented themselves to a
mind capable of developing them into the most efficient form of telegraphic
apparatus which we possess. In October, 1832, among the passengers
on board the steamship Sully, bound from France to the United States,
was a talented American artist who had gained some reputation in his
profession. A casual conversation with his fellow-passengers on electricity,
and the plan by which Franklin drew it from the clouds along a slender
wire, suggested to the artist the possibility of thus communicating intelligence
by signals at a distance. He named his notion to a fellow-passenger,
Dr. Jackson, an American professor, who had devoted some attention to
electrical science, and this gentleman suggested several possible (and impossible)
methods in which the thing might, as he thought, be accomplished.
None of these suggestions, however, indicated the direction in
which the idea afterwards took practical form in Morse’s hands. Jackson
had among his baggage in the hold, and therefore inaccessible on the
voyage, a galvanic battery and an electro-magnet, and these he described
to the painter by the aid of rough sketches. When, some years afterwards,
Morse had realized his ideas of electric communication, and success was
bringing him the favour of fortune, Jackson advanced a claim to a share
in the invention, and a famous lawsuit, Jackson v. Morse, was ended by
a verdict in favour of Morse, which public and scientific opinion has
unanimously endorsed. In reference to this matter, Mr. R. Sabine, the
author of an excellent little treatise on “The History and Progress of the
Electric Telegraph,” has thus placed the subject in its true light:
“Two men came together. A seed-word, sown, perhaps, by some purposeless
remark, took root in fertile soil. The one, profiting by that which
he had seen and read of, made suggestions, and gave explanations of
phenomena and constructions only imperfectly understood by himself, and
entirely new to the other. The theme interested both, and became a subject
552of daily conversation. When they parted, the one forgot or was indifferent
to the matter, whilst the other, more in earnest, followed it up
with diligence, toiling and scheming ways and means to realize what had
only been a dream common to both. His labours brought him to the
adoption of a method not discussed between them, and Morse became the
acknowledged inventor of a great system. Fame and fortune smiling upon
the inventor, it was natural enough that Jackson, awakening from his unfortunate
indolence, should remember his share in their earlier interchange
of ideas, that had, perhaps, first directed Morse’s attention to the subject
of telegraphy. And, although we are compelled to pronounce dishonest
those attempts which Jackson made to claim the later and proper invention
of Morse—that of the electro-magnetic recorder—and strong as is our
confidence in the spotless integrity of our friend, we cannot entirely ignore
Jackson—little as he has done—nor deny him an inferior place amongst
those men whose names are associated with the history and progress of the
electric telegraph in America.”
From the time of this chance conversation with Dr. Jackson, Morse
devoted his mind entirely to the subject of telegraphic communication,
and although then more than forty years of age, he abandoned the profession
in which he had already gained some distinction, and with the energy
and elastic power of adaptability which characterize the American mind, he
gave himself up to this new pursuit to such good purpose, that a few years
afterwards saw his telegraph system completely established in the United
States, where the lines now exceed 20,000 miles in length. At the instigation
of the late Emperor of the French, the Governments of France,
Belgium, Holland, Austria, Sweden, Russia, Turkey, and the Papal States,
combined to award to Professor Morse, in recognition of his services to
practical science, the sum of £16,000. It was in 1836 that Morse had first
brought his notions into a practical form, but his apparatus has since
received many improvements at his own hands, or by the useful modifications
of it which have been proposed by others. The transmitting key
invented by Morse has proved a valuable piece of apparatus, and its
simplicity has contributed much to the success of his invention. Telegraphs
on this system were erected in America in 1837, and the Morse
apparatus is now more extensively used than any other in every country.
In 1840 Professor Wheatstone had succeeded in most ingeniously applying
electro-magnetism in such a manner as actually to realize Strada’s
sympathetic needles, by having the letters of the alphabet arranged round
the circumference of a circle, and pointed at by a revolving hand. Such a
dial is provided at each end of the line, and the sender of the message
has only to make the index of his own dial pause for an instant at any
letter; the hand of his correspondent’s dial will also pause at the same
letter. These dial telegraphs are particularly convenient for many purposes,
as they do not require a trained telegraphist to read or send the
messages. Wheatstone’s plan has been greatly simplified by Breguet, of
Paris, and others, and it is much used in mercantile and public establishments.
From the foregoing discursive historical indication of the progress
of the electric telegraph we shall now proceed to describe the systems
most commonly employed in practical telegraphy, with a brief reference
to some other interesting forms; and in following these descriptions, the
reader will find the advantage of an acquaintance with the electrical facts
discussed in the last article, with which facts we shall presume he has
become to a certain extent familiar.
553In every telegraphic system there are three distinct portions of the
apparatus, which may be separately considered, as they may be variously
combined. We have—
1º. The apparatus for producing the electricity, such as batteries, magneto-electric
machines, &c.
2º. The conductors, or wires, which convey the electricity.
3º. The apparatus for sending and for receiving the messages.
Of the first we shall have little to add to what has been said in the last
article; and before entering upon the description of the second, it will be
better to discuss the third division.
Telegraphs may conveniently be classed according to the mode in
which the actions of the sender produce their effect at the point where
the message is received. A first class may include those in which the current
is made to deflect magnetized needles; a second may comprise those
in which the current, by magnetizing soft iron, causes an index to travel
along a dial and point to the letter intended; a third may embrace those
in which the same action on soft iron is made to print the despatches, either
in ordinary type or in conventional signs; while in a fourth class we may
put the instruments which give their indications by sounds only. It is
obvious that in some of these systems signs only are used, and a special
training and acquaintance with the symbols is necessary, while in the rest
the ordinary alphabetic letters are shown or recorded. In the former case
the apparatus is simpler, and therefore for the general business of public
telegraphy it is almost exclusively employed; while for private purposes,
where it is often required that the messages should be dispatched and
received by persons not acquainted with the symbolic language, the dial
telegraph, or that which prints the message in ordinary characters, will
continue to be employed, in spite of the greater complexity and greater
liability to derangement of the apparatus.
In the needle telegraphs the essential part of the apparatus is a multiplier
(page 493), having its needle mounted vertically on a horizontal axis, to
which is also attached an indicator, visible on the face of the instrument,
and formed either of a light strip of wood, or of another magnetized needle,
having its poles placed in the reverse position to those of the needle within
the coil. When the current is sent through the latter, the index is deflected
to the right or left, according to the direction in which the current passes.
Fig. 282 represents the exterior of one of Wheatstone and Cooke’s double-needle
instruments, now almost entirely superseded, where needles are used
at all, by the single-needle instrument. The face of the instrument is
marked with letters and signs, which were supposed to aid the memory of
the telegraphist, and the movements of the needles were chosen rather
with that view than any other. We need not here give the code of signals,
as the double instrument is now obsolete, and the code for the single-needle
instrument, which was devised by Wheatstone and Cooke, has been in
most cases superseded by one corresponding with the Morse code, a deflection
to the right representing a dot, and a deflection to the left a dash.
554
Fig. 282.—The Double-Needle Instrument.
The smaller case surmounting the instrument, Fig. 282, contains a bell
or alarum, which serves to call the attention of the clerk at the receiving
station. The first electric bell-alarum was invented by Wheatstone and
Cooke. It was simply a clock alarum, put in motion by a wound-up spring.
The spring was released at the proper moment by a detent, which was
removed by the attraction of a soft iron armature to the core of a small
electro-magnet, formed by the line wire itself; but when the current, on
account of the length of the line, was too weak to produce a sufficiently
strong electro-magnet, Wheatstone caused it to close the circuit of a local
battery. The electric alarum has been modified in a thousand ways, and
as electric alarums or bells are now coming into common use in hotels, and
even private houses, we give in Fig. 283 a representation of one of the simplest
forms, in which the bell is rung continuously by the electric current so
long as the circuit is closed. The action is very simple: a soft iron armature,
A, is attached to the steel spring, B, and prolonged into a hammer, C,
which strikes the bell, D, every time the armature is attracted to the electro-magnet.
The armature and the spring, E, form part of the circuit, which
is continued by connectors to F, and through the coils to G. The spring,
E, does not follow the armature in its motion towards the electro-magnet,
and consequently the circuit is broken before the armature touches the
magnet; but the hammer strikes the bell, and the elasticity of the spring,
555B, brings the armature back into contact with E, the circuit is closed, and
the motions are repeated, so that the bell is struck a rapid succession of
blows. This make-and-break movement is precisely similar to that with
which Ruhmkorff’s coils are usually provided.
Fig. 283.—Electro-Magnetic Bells.
Below the dial of the instrument, in Fig. 282, may be seen two handles.
Each of these is connected with an arrangement constituting the transmitting
apparatus, by which the metallic contacts are varied according to the
position of the handles. When the handle is vertical, all communication
with the battery in connection with the instrument is cut off, but the coils
are ready to receive any current from the line-wires. When the handle is
turned to the right or left, the contacts are such that the battery current
flows into the line, and deflects to the right or left the needles of both
receiving and transmitting instruments. The single-needle instrument as
now made is of a very simple and inexpensive construction, and it is the
form principally used in connection with the working of lines of railway.
One may see at every station in the United Kingdom the little vertical
needle, mounted in the centre of a small perfectly plain green dial-plate;
for the letters and signs with which it was formerly the practice to cover the
dial have been found to distract the eye more than they aid the memory.
A boy will after a few weeks’ practice learn to read the signals and to
transmit messages with considerable rapidity.
Fig. 284.—Portable Single-Needle Instrument.
The field telegraph lines, which are used in actual warfare to enable the
commander of an army to communicate with every part of his forces, require
as the essential condition for their construction rapidity of erection
and removal, and the greatest possible simplicity and portability in the
sending and receiving instruments. The wires are fastened to trees, or
other fixed supports, where such are available, but artificial supports are
provided in light poles which admit of being readily planted in the ground
556and removed. In cases where it is inexpedient or impossible to use these,
the conductor may be laid along the ground, but must then be well insulated
with some non-conducting material, which is capable of withstanding
the action of the weather. A kind of cable is usually employed, in which
is the conductor, made of copper, protected and strengthened by hemp
fibres and covered with some non-conducting material. No form of needle
telegraph instrument could be simpler than that represented in Fig. 284,
which has been designed for military purposes. The communicator, or
transmitting apparatus, here shows an arrangement very compact, and not
easily deranged. The springs, AB, press against the piece of metal marked
C, with which good contact is insured by providing the springs with several
projecting steel points. D, E are finger-keys of ebonite or ivory; underneath
are two points of a metallic conductor on which the springs can be pressed
down by a touch of the finger. This conductor is in communication with
the binding-screw, F, from which a wire proceeds to the negative or zinc end
of the battery, while the piece, C, is in metallic connection with G, to which
a wire proceeding to the positive or copper end of the battery is attached.
From B a wire, H, communicates through the hinge with one end of the
coil, the upper end of which is connected through the upper hinge with a
binding-screw not visible in the figure, and to this the end of the line conductor
is attached. From A a wire K passes to another binding-screw,
by which the earth connection is made. A current arriving by the line
traverses the coils and passes through H and B into C, hence by A into the
earth through K. When D is depressed the current from the battery passing
from G through C, A, and K, into the earth, and thus to the distant
557station, returns through the coils of the instrument there and along the line
wire, through the coils, L L, and by H, B, D and F, to the negative pole of
the battery. The reader will have little difficulty in tracing the course of
the reverse currents, whether sent or received, which deflect the needles
in the opposite direction.
The field telegraph instrument selected by the War Department of the
United States Government is also extremely simple, communicating its
signals, not by the deflections of a needle, but by the blows on an electro-magnet
of its armature. The letters are indicated by various combinations
of two signals—one, a single stroke of the armature; and the other, two
blows in very rapid succession. The alphabet used is the “General Service
Flag Code” of the American army and navy, and the signal numerals
of this code are indicated by contacts of the transmitting key—one contact
producing a single blow of the armature, implying the numeral 1, and two
rapidly succeeding contacts causing two blows, which stand for the numeral
2. The signals are read merely by the sound made by the stroke of the
armature. In the table below the code is given, dots being used to represent
the contacts of the key in the “sending” instrument, and the blows
of the armature in the “receiving” instrument—the single dots standing
for one contact or sound, and the double dots for the double blows:
Letters.
Flag Code.
Telegraph Signals.
A
2 2
·· ··
B
2 1 1 2
·· · · ··
C
1 2 1
· ·· ·
D
2 2 2
·· ·· ··
E
1 2
· ··
F
2 2 2 1
·· ·· ·· ·
G
2 2 1 1
·· ·· · ·
H
1 2 2
· ·· ··
I
1
·
J
1 1 2 2
· · ·· ··
K
2 1 2 1
·· · ·· ·
L
2 2 1
·· ·· ·
M
1 2 2 1
· ·· ·· ·
N
1 1
· ·
O
2 1
·· ·
P
1 2 1 2
· ·· · ··
Q
1 2 1 1
· ·· · ·
R
2 1 1
·· · ·
S
2 1 2
·· · ··
T
2
··
U
1 1 2
· · ··
V
1 2 2 2
· ·· ·· ··
W
1 1 2 1
· · ·· ·
X
2 1 2 2
·· · ·· ··
Y
1 1 1
· · ·
Z
2 2 2 2
·· ·· ·· ··
There are similar signals for the numerals and for a few often-recurring
syllables.
The telegraphs we have hitherto described leave no record of the despatches
sent, and hence the messages cannot be read at leisure, and errors
which may occur in the transmission cannot be traced to their source. A
system which registers the messages as actually received has plainly many
advantages over those which merely give a visible or audible signal without
leaving any trace. Hence many contrivances have been proposed for
making the receiving apparatus print the message in ordinary characters.
Such instruments are necessarily very much more complicated in their
construction than those we have already mentioned, and by no means so
simple as the system we are about to describe, namely, the Morse Telegraph,
which is now so largely used, being universally adopted in America
and on the continent of Europe; and, since the telegraphic communication
558in Great Britain came into the hands of the Post-office authorities, here,
also, the Morse is the system most approved.
Fig. 285.—Connections of a Telegraphic Line, with Morse Instruments.
The general arrangement of the transmitters, batteries, receiving instruments,
&c., should be first studied in its simplest form, as represented by
the diagram, Fig. 285. M represents the vertical coils of an electro-magnet
upon which we are supposed to be looking down; the armature, A, is
attached to a lever, F, which, by the attraction of the electro-magnet is therefore
drawn down. In the position of the connections, as represented, no
current is passing, but if K be pressed down so as to make connection at 1,
at the same time it is broken at 2, a current will pass in from the positive pole
of battery, B, into the line by 1, 3, L, L´, and through 3´, 2´ through the
coils of the electro-magnet at M´ into the earth, and so back to the negative
pole, Z. The armature, A´, will be attracted so long as the current continues.
Similarly, contact made at 1´ and broken at 2´, will affect the
electro-magnet, M, from the battery at B´. It should be noticed here that
it is not a question of the reversal of currents sent from the same battery;
the key merely enables the operator to send a current in one direction, so
as to affect the distant electro-magnet whenever or so long as he depresses
the key. We shall now examine the construction of the Morse receiving
apparatus, one of the most complete forms of which is depicted in Fig. 286.
In the present description we wish the reader to consider only the portion
of the apparatus towards the left, and to suppose the absence of the electro-magnet
at the right-hand side, with all the appliances immediately connected
with it. He must regard the electro-magnet, A, as corresponding
with M´ in Fig. 285, and remember that it is in the power of the distant
operator at K to throw the current of his battery through the coils of A,
by simply depressing his key. When the current passes the armature, B,
it is attracted, and the lever, C, to which it is attached, turns on its bearings
at D, and the end, E, of its longer arm is pressed upwards. At this
end of the lever, in the earlier form of the instrument, was a blunt steel
point which, while the armature was attracted to the electro-magnet, was
559pressed into a shallow groove in a metallic roller. Between the roller and
the steel point a paper ribbon, half an inch wide, K, was unwound from
the drum, L, by the two rollers, M and N, which grip the paper between
them as they are turned by clockwork within the case, F.
Fig. 286.—Morse Recording Telegraph.
An important improvement was effected when, instead of steel points
for embossing the message, the Morse instrument was provided with an
arrangement for printing the signals in ink; since the pressure required
for embossing the paper is considerably greater than that needed merely
to bring it into contact with the edge of a little inked disc. In the inking
arrangement the strip of paper travels just below the margin of a vertical
disc, turned by the clockwork, and having its plane parallel to the length
of the paper strip. The narrow edge of this disc is kept charged with
printer’s ink, which it receives from a roller. The end of the lever connected
with the armature of the electro-magnet is formed of a light strip
of metal carrying a narrow projection at the end, over which the paper
passes, just beneath, but not touching, the inking disc. When the current
passes, the little projection is lifted up, and raises the paper into contact
with the ink, printing either a dot or a dash according to the duration of
the current. The amount of force required to raise an inch or two of the
length of the paper ribbon through a space not greater than the twentieth
of an inch is but small, and much less than would be required to
emboss the paper; so that in a great many cases the part of the apparatus
which is represented in Fig. 286, on the right, may be dispensed with.
In other cases it is, however, necessary; as when, from the length of the
line, the currents are too feeble to give clear indications with the printing
lever; and we shall, therefore, presently describe its arrangement and
purpose.
The clockwork is actuated by a spring, wound by the handle G, but its
560action is suspended by a detent, which is released by touching the lever H.
When the clockwork is in action and the current constantly circulating in
the coils, a continuous line, parallel to the length of the ribbon, would be
printed upon it, in consequence of the contact with the inking-disc, P, being
maintained; but when a momentary current only rushes through the coils,
the armature attracted but for an instant, gives rise to merely a dot on the
passing paper, while a current of a little duration will cause the paper to
be marked with a short line or dash.
The dot and the dash are the elementary signs of the Morse code of
signals, and these are producible according to the time the contact key is
held down at the distant station. By employing various combinations of
these two signs, the letters of the alphabet, numerals, &c., are indicated.
In selecting the combinations Professor Morse had regard to the frequency
with which the different letters recur in the English language. Thus, for
the letter E, which is more frequently used than any other, the symbol
chosen was a single dot; and for T, which is the next most frequently employed,
the dash was plainly the most appropriate; then the four only
possible combinations of the signs in pairs fell to the next most frequent
letters, and so on. The following table gives the complete Morse code.
The eye of the reader will doubtless detect a kind of symmetry in the
arrangement of the signs for the first five and last five numerals:
6. To be placed between the numerator and denominator of a vulgar fraction.
7. To be placed before and after the words to which they refer.
OFFICIAL SIGNALS.
Sign.
Public message
···
Official Telegraph message
·-
Private message
·--·
Call
-·-·-·-
Correction, or rub out
···-·
Interruption
·········
Conclusion
·-·-·-·
Wait
·-···
Receipt
·-··-··-·
The length of a dot being taken as a unit, the length of a dash
= 3 dots.
The space between the signs composing a letter
= 1 dot.
The space between two letters of a word
= 3 dots.
The space between two following words
= 6 dots.
Fig. 287.—Morse Transmitting Key.
Fig. 288.—Morse Transmitting Plate.
Fig. 287 is a view of the Morse transmitting key. A B is a brass lever,
moving in bearings at C, and provided at the end of its longer arm with a large
knob or button of some insulating material. Steel pins are screwed in at B
and D, and they are so adjusted that while that at B is pressed against the
562projection, E, by the action of the spring, F, when the knob, K, is pressed,
contact is broken at B, and established at D. D and E are each provided
with a binding-screw, so that wires may be attached in the manner indicated
in Fig. 285. When the key is in the position shown, a current arriving
by the line-wire passes from the fulcrum, C, of the lever through the contacts
into the apparatus. When the knob is pressed down the battery current
enters the lever by the contact at D, and passes into the line from the
fulcrum, C. The clerks who are called upon to transmit messages usually
soon learn to time the contacts very accurately in accordance with the code
of signals, so as to produce the dashes and lines with accuracy. However,
with certain persons some difficulty was found in acquiring the requisite
uniformity, and to obviate any objection on this score, Morse invented an
arrangement for facilitating the signalling, which is represented in Fig. 288.
This is a smooth tablet of a non-conducting substance, such as ivory, except
the shaded portions, which are plates of metal having their surfaces
even with that of the ivory, and all soldered to a plate of metal beneath
the ivory, which places them all in communication with each other and with
563the binding-screw, C. The lengths of the strips of metal and those of the
spaces between them correspond with the dots and dashes of the Morse
alphabet as marked on the tablet. The battery wire is connected with the
binding-screw, C, and the line-wire terminates in an elastic and flexible
coil of insulated wire, which is attached to a short rod having an insulated
handle and terminated by a blunt platinum point. This the transmitter
takes in his hand and draws uniformly along the line of metal strips
belonging to the letter which he wishes to telegraph. The circuit is closed
while the point of the style is passing across the metallic strips. This
arrangement appears to be but little used, but it is nevertheless admirable
for its simplicity, and is described here as a good illustration of the mode
in which the varied duration of the contacts is able to produce the signals
of the Morse alphabet. With the ordinary transmitting key a clerk is able
to telegraph, on the average, twenty or twenty-five words in a minute, but
the receiving apparatus is capable of recording three times as many. Morse
also invented a system of transmitting the messages automatically, by setting
up the message in a kind of type, just as ordinary letters are arranged
for printing. The type, if it may be so called, had simple projections like
the slips of metal, corresponding with each letter in Fig. 288. The lines of
the message were drawn under a contact-lever, which closed the circuit
when lifted up by the projections. Thus the speed of transmission could
be very greatly increased, and a single wire and apparatus had its capacity
of conveying a great number of messages in a given time proportionately
enlarged.
We have now to ask the reader’s attention to the details of the apparatus
in Fig. 286, the use of which has not already been pointed out. The electro-magnet,
O O´, and the parts immediately connected with it, form what is
called a relay. The object of this may be illustrated by supposing that
the instrument is at one end of a long line, such as that between Edinburgh
and London. Let us suppose it is at Edinburgh: the currents sent from
London by a battery of convenient size might not be powerful enough to
magnetize the soft iron of A with sufficient intensity to give clearness to
the signals. They are, therefore, made to circulate in the electro-magnet,
O, where they act by attracting the armature, W, which has the form of a
split tube of soft iron, attached to a very light lever, Q, adjusted with great
delicacy, and so that it moves by little magnetic force. The end of the
lever works between two adjustable screws, R and S, which are electrically
insulated, except that R is in communication with one extremity of the
coils of the electro-magnet, A. Q is in metallic communication through the
pillar, T, and the binding-screw, U, with the zinc end of a battery at Edinburgh,
which is called the local battery, the other pole of which communicates
with the other ends of the coils, A, through the screw, U´. When no
current from London is passing through O, Q is held down by the spring,
W´, and the circuit of the local battery is broken; but the instant the line-current
passes, the armature, W, is attracted, and Q makes contact with R,
the current from the local battery rushes through the coils, A, and the
appropriate movements of the printing lever are effected by its action. X
is a spring for drawing down the lever, and it is provided with a screw for
adjusting its tension, and Y, Z, are screws for limiting the extent of motion
of the lever; under P is the little projection by which the band of paper is
pressed against the inking-disc; l and e are respectively the screws for the
line and earth connections.
An extremely ingenious system of signalling, by which the speed could
564be greatly increased, has been devised by Sir Charles Wheatstone, and is
largely adopted by the British postal authorities. In this system the message
is first translated into telegraphic language by a machine, which
punches certain holes in a strip of stiff paper. The apparatus originally
designed for this purpose by the inventor is thus described by him in the
Juror’s Report, International Exhibition of 1862:
“Long strips of paper are perforated by a machine constructed for the
purpose, with apertures grouped to represent the letters of the alphabet
and other signs. A strip thus prepared is placed in an instrument associated
with a source of electric power, which, on being set in motion, moves
it along, and causes it to act on two pins in such a manner that when one
of them is elevated the current is transmitted to the telegraphic circuit in
one direction, when the other is elevated it is transmitted in the reverse
direction. The elevations and depressions of these pins are governed by
the apertures and intervening intervals. These currents, following each
other indifferently in these two opposite directions, act upon a writing
instrument at a distant station in such a manner as to produce corresponding
marks on a slip of paper, moved by appropriate mechanism.
“The first apparatus is a perforator, an instrument for piercing the slips
of paper with the apertures in the order required to form the message.
The slip of paper passes through a guiding groove, at the bottom of which
an opening is made sufficiently large to admit of the to-and-fro motion of
the upper end of a frame containing three punches, the extremities of which
are in the same transverse line. Each of these punches, the middle one
of which is smaller than the two external ones, may be separately elevated
by the pressure of a finger-key.
“By the pressure of either finger-key, simultaneously with the elevation
of its corresponding punch, in order to perforate the paper, two different
movements are successively produced: first, the raising of a clip which
holds the paper firmly in its position; and secondly, the advancing motion
of the frame containing the three punches, by which the punch which is
raised carries the slip of paper forward the proper distance. During the
reaction of the key consequent on the removal of the pressure, the clip first
fastens the paper, and then the frame falls back to its normal position.
The two external keys and punches are employed to make the holes, which,
grouped together, represent letters and other characters, and the middle
punch to make holes which mark the intervals between the letters.
“The second apparatus is the transmitter, the object of which is to
receive the slips of paper prepared by the perforator, and to transmit the
currents in the order and direction corresponding to the holes perforated
in the slip. This it effects by mechanism somewhat similar to that by
which the perforator performs its functions. An eccentric produces and
regulates the occurrence of three distinct movements: 1. The to-and-fro
motion of a small frame which contains a groove fitted to receive the slip
of paper, and to carry it forward by its advancing motion. 2. The elevation
and depression of a spring-clip, which holds the slip of paper firmly
during the receding motion, but allows it to move freely during the advancing
motion. 3. The simultaneous elevation of three wires placed parallel
to each other, resting at one of their ends over the axis of the eccentric,
and their free ends entering corresponding holes in the grooved frame.
These three wires are not fixed to the axis of the eccentric, but each end
of them rests against it by the upward pressure of a spring; so that when
a light pressure is exerted on the free end of either of them, it is capable
565of being separately depressed. When the slip of paper is not inserted
the eccentric is in action; a pin attached to each of the external wires
touches during the advancing and receding motions of the frame a different
spring; and an arrangement is adopted, by means of insulation and
contacts properly applied, by which, while one of the wires is elevated, the
other remains depressed; the current passes to the telegraphic circuit in
one direction, and passes in the other direction when the wire before elevated
is depressed, and vice versâ; but while both wires are simultaneously
elevated or depressed the passing of the current is interrupted. When
the prepared slip of paper is inserted in the groove, and moved forward
whenever the end of one of the wires enters an aperture in its corresponding
row, the current passes in one direction, and when the end of the other
wire enters an aperture of the other row, it passes in the other direction.
By this means the currents are made to succeed each other automatically
in their proper order and direction to give the requisite variety of signals.
The middle wire only acts as a guide during the operation of the current.
“The wheel which drives the eccentric may be moved by the hand, or by
the application of any motive power. Where the movement of the transmitter
is effected by machinery, any number may be attended to by one
or two assistants. This transmitter requires only a single telegraphic wire.
“The third apparatus is the recording or printing apparatus, which
prints or impresses legible marks on a strip of paper, corresponding in
their arrangement with the apertures in the perforated paper. The pens
or styles are elevated or depressed by their connection with the moving
parts of the electro-magnets. The pens are entirely independent of each
other in their action, and are so arranged that when the current passes
through the coils of the electro-magnet in one direction, one of the pens is
depressed, and when it passes in the contrary direction the other is depressed;
when the currents cease, light springs restore the pens to their
elevated points. The mode of supplying the pens with ink is the following:
A reservoir about an eighth of an inch deep, and of any convenient
length and breath, is made in a piece of metal, the interior of which may
be gilt in order to avoid the corrosive action of the ink; at the bottom of
this reservoir are two holes, sufficiently small to prevent by capillary attraction
the ink from flowing through them; the ends of the pens are placed
immediately above these small apertures, which they enter when the electro-magnets
act upon them, carrying with them a sufficient charge of ink to
make a legible mark on a ribbon of paper passing beneath them. The
motion of the paper ribbon is produced and regulated by apparatus similar
to those employed in other register and printing telegraphs.”
The mode by which Wheatstone proposed to indicate the letters was
novel, consisting in dots only, the numbers and positions of which in two
lines along the paper ribbon distinguished the letters—the system of combining
the symbols being still identical with the Morse code, only the dash
was replaced by a dot in the lower lines:
WHEATSTONE’S DOT SIGNALS.
˙⠄
⠄˙˙˙
⠄˙⠄˙
⠄˙˙
˙
˙˙⠄˙
⠄⠄˙
˙˙˙˙
˙˙
˙⠄⠄⠄
A
B
C
D
E
F
G
H
I
J
MORSE’S DOT AND DASH.
·-
-···
-·-·
-··
·
··-·
-·
····
··
·-
A
B
C
D
E
F
G
H
I
J
566A single dot in the upper line stood for E, in the lower line for T; a dot in
the upper line, followed by one in the lower line a little to the right, represented
A; one in the lower line, followed by another in the upper line, indicated
N; and so on. By the dot printing it is said that Wheatstone would
signal 700 letters per minute. There were, however, objections to the new
code of signals: all the world had agreed to use the Morse alphabet, and
it was perhaps less liable to incorrect reading; and for other reasons this
more rapid signalling was unsuitable for submarine lines. The apparatus
has therefore been modified to suit the dot and dash system of signals, and
great improvements have been effected by Sir Charles on the original instruments,
with a view of increasing the rapidity of transmission as much
as possible. The paper as punched for the Morse signals shows a row of
equidistant holes in the middle, by which the paper is guided uniformly
forward, and in the outer rows are holes arranged in pairs, either exactly
opposite to each other or obliquely—the former produce dots at the receiving
station, the latter dashes. From 60 to 100 words can thus be sent
and printed in one minute, and the automatic transmitting system can be
applied to the needle, or any other form of telegraph.
After a clerk has for some time been habituated to working with the
Morse instrument, he is able to read the message from the different sounds
made by the armature, as dashes or dots are respectively marked, and he
usually listens to the message, and transcribes it at once into ordinary
language by the ear alone. This observation soon led to the adoption of
sound alone as the means of signalling, and an instrument on this plan has
already been referred to.
Among the more remarkable forms of recording telegraphs, that of Hughes
may be mentioned, in which the message is printed at the receiving station
in distinct Roman characters; and as only a single instantaneous current
is required to be sent for each letter, the speed with which a message can
be dispatched is about three times as great as with the Morse instrument.
These advantages are, however, obtained only at the cost of great delicacy
and complexity in the apparatus, so that it is unfit for ordinary use, although
it is much employed on important lines, where competent operators and
skilled mechanics and electricians are at hand to keep it duly regulated.
This machine is too complicated for a full description in these pages,
although it is the best form of type-printing telegraph, and possesses a
special feature in the fact that the printing is done whilst the wheel carrying
the types is in rapid rotation. The reader will find full and untechnical
descriptions of this and of all the more important forms of telegraphic
apparatus in Mr. R. Sabine’s useful “History and Progress of the Electric
Telegraph,” or in Lardner’s work as edited by Sir Charles Bright.
Fig. 289.—The Step-by-step Movement.
Fig. 290.—Froment’s Dials.
From the numerous forms of dial telegraphs we select two for description.
All these instruments are characterized by what is called the “step-by-step”
movement, and differ in their mechanical details, and in the
nature of the apparatus for producing the currents, some being driven by
electro-magnets and others by galvanic batteries. Their principle may be
easily explained. Suppose that a ratchet-wheel, having twenty-six teeth,
is mounted on an axis carrying a hand over a dial having the letters of the
alphabet inscribed upon it. A simple arrangement in connection with an
electro-magnet, somewhat like the escapement of a clock, will serve to
advance the wheel by one tooth each time a current passes. The diagram,
Fig. 289, will at once make this principle clear. E is the electro-magnet,
F the armature, separated by the spring, S, from the magnet, except when
567the current passes, when the catch, C, draws down the tooth in which it is
engaged, so that a tooth passes under the point at D; and when the current
ceases, the spring, S, brings up the catch to engage the succeeding tooth,
and thus the hand moves step by
step in the direction of the arrow,
advancing each time the electric circuit
is closed by one twenty-sixth of a
revolution. In Fig. 290 is represented
lecture-table models of a step-by-step
indicating and transmitting instrument,
as constructed by M. Froment,
of Paris. These instruments are supposed
to be at the extremities of a
long line of wire. The left-hand
figure is the manipulator, or sending
instrument, in which the operator has
merely to quickly turn round the
index in the direction of the hands
of a watch, by means of the knob, P,
until it points to the desired letter,
pause at the letter for an instant, and
then quickly continue the movement
until his index points to the cross at
the top of the dial, where he pauses
if the word is spelt out, and, if not,
continues the rotation until he arrives at the next letter, and so on. All
these movements and pauses the hand on the indicator will accurately
repeat, and the reason of this may be seen by observing that the battery
contacts are made by the projections on the metallic wheel, R, which turn
568with the index. The spring, N, is always in contact with the wheel, but
the spring, M, has such a shape that contact is alternately made and broken
as the projections and spaces pass it. It is obvious that the needle of the
indicator will therefore advance over the same letters as the index of the
communicator.
Fig. 291.—Wheatstone’s Universal Dial Telegraph.
A very elegant dial instrument has been invented by Sir Charles Wheatstone,
in which magneto-electric currents are made use of. In Fig. 291
communicator and indicator are represented mounted in one case, or small
box. The larger dial is the communicator, and its circumference is divided
into thirty equal spaces, in which are the twenty-six letters of the alphabet,
three punctuation marks, and a +. In an inner circle are two series of
numerals and other signs. About the circumference of the dial are thirty
small buttons or projecting keys, conveniently arranged, so as to be readily
depressed by the touch of a finger. Inside of the box a strong permanent
horse-shoe magnet is fixed, and near its poles a pair of armatures of soft
iron cores with insulated wire coils revolve when the handle, A, is turned,
as in the machines described in the last article. In this manner a series
of waves or short currents of electricity are produced in the conductors
when the circuit is complete, and the currents are alternately in opposite
directions, so that fifteen revolutions of the coils will produce fifteen currents
in one direction and fifteen in the other. A pinion on the same
spindle as the coils works with a wheel on the axis carrying the pointer
on the dial, so that the pointer makes a complete revolution as often
as the handle, A, makes fifteen turns. Each of the thirty currents
will pass through the indicator, I, and through the line to the distant station,
where they will, by a step-by-step movement, advance the needle of
the indicator. So that the hand of the dial and the needle of the indicator
at the sending station, and that of the indicator at the distant station, will
569all simultaneously be pointing to the same letter on their respective dials;
and they would continue to move round these, ever pointing to the same
letter, so long as the handle, A, is turned. How, then, is the sender to cause
the needle of his correspondent’s instrument to pause at any desired letter?
Not by stopping the revolution of the handle, A, for that could not be done
so as to send just the right number of currents, inasmuch as the rotating
armatures could not be instantly stopped. The mode of causing the indicators
to pause at any required letter is as simple as it is ingenious. It has
been already mentioned that the step-by-step movement takes place at
every current which passes through the line, including the two indicators,
and that thirty such currents pass at each revolution of the pointer of the
communicator. But when these currents no longer flow, the indicators, of
course, stop; and the stoppage of the movements is reconciled with the
continuous production of the currents by having a series of little levers,
each connected with one of the buttons, and so arranged that when one of
these has been pushed down, the lever stops the revolution when it has come
round of an arm on the same central axis as the pointer, and riding loosely
on a hollow spindle, which bears the toothed wheel, driven by the pinion
already spoken of. The projecting arm is provided with a spring, which
falls between the teeth of the wheel, so that the arm is with certainty carried
round with the wheel. But where a button has been pushed down, its
lever catches the arm, lifting its spring away from the teeth of the wheel.
So long as the key remains down, the arrested arm makes a short metallic
circuit by its contact, and no currents pass into the line, for they take
the shortest path. The key is raised only when another is depressed,
and then the arm and the pointer immediately resume their revolution
until they again become stationary at the letter corresponding with the key
which has been pushed down. Suppose the key of +, the zero of the dial,
to be down, which is the proper condition of the apparatus when a message
has to be dispatched. The operator having rung a bell at the distant
end, to call the attention of the person who receives his message, begins
to turn the handle, A, at the rate of about two revolutions per second. In
this state of affairs no current is passing into the line, and the fingers of
both his communicator and indicator remain stationary, as does also that
of the indicator at the distant end of the line. Now, suppose he has to
spell the word “FOX.” He turns the handle A continuously with his
right hand the whole time he is sending the message; and, manipulating
the keys with his left, he depresses that opposite to the letter F. By this
action the key opposite + is raised, for the levers are pressed into notches
against a watch-chain, which has just enough slack to allow one lever
to enter a notch, and therefore the pressure of another lever always raises
the key last depressed. When the operator presses down the F key, the +
rises, the radial arm is instantly released, and with the index is carried on
to F, where it stops; and the contacts will have, during that movement,
sent six currents into the line, so that the fingers of both indicators will
also point to F. When the pointer of the communicator has made just a
visible pause at F, he pushes down the key of O, and all the three pointers
recommence their journeys towards that letter. The operator must, of
course, wait until they have reached it and paused an instant, when he
depresses the button opposite X; and when the index has pointed at that,
he pushes down the + key, whereby the fingers all arrest their movements
at that point, indicating that the word is completed. In the case supposed
the word is completed by a single revolution of the pointers; but this is,
570of course, not usually the case; thus, in indicating the syllable “PON,”
nearly three complete revolutions would be required.
This admirable little instrument was designed for the use of private
persons, and is largely used in London and elsewhere. Its great compactness
and simplicity of operation render it highly suitable for this purpose.
There is no battery required, and all the inconvenient attention demanded
by a battery is therefore dispensed with. On the other hand, the magnets
gradually lose their power, and after a time must be re-magnetized; and
the electro-motive force developed in these instruments is insufficient for
lengths of line much exceeding 100 miles. For shorter lines, and for the
purposes for which they are designed, these instruments are perfection.
Very interesting forms of telegraph are those in which a despatch is not
merely written or printed, but actually transcribed as a facsimile of the
writing in the original; and in this way it is possible for a design to be
drawn telegraphically at the distance of hundreds of miles. Like the
Hughes’ printing telegraph, the instruments which produce these apparently
marvellous results require synchronous movements at the two
stations. But although they are scientifically successful, there appears to
be no public demand for these copying telegraphs. One of the best known
is Bonelli’s, which dispatches its messages automatically when they have
been set up in raised metal types precisely similar to the Roman capitals
in the type of the ordinary printer. In Bonelli’s and most other copying
telegraphs the impressions are produced by chemical decompositions—effected
at the receiving station on the paper prepared to receive the message.
By Bonelli’s instrument it is said that when the type has been set
up, messages can be sent at the extraordinary rate of 1,200 words in one
minute of time! The action of this system is such that it is proved to be
possible to reproduce in a few seconds—at York, say—the very characters
of a page of type the moment before set up in London. The limits of our
space will not admit of details of this invention; but we here place before
the reader a facsimile of the letters printed by it at the receiving stations.
We have to describe two other forms of instruments for receiving telegraphic
signals, both contrived with consummate skill by Sir William
Thomson, and, though exhibiting no new principle in any of their parts,
both fine examples of beautiful adjustment of materials for a desired end.
In these forms of apparatus, the delicacy of the mechanical construction,
and the accurate relations of one part to another, have produced results of
the greatest practical importance. Fig. 292 represents the mirror galvanometer,
an instrument which has not only proved of the highest value in
scientific researches, but is of the first importance in submarine telegraphy.
It is in principle nothing more than the single-needle telegraph, and it is
exceedingly simple in construction. A very small and light magnet, such
as might be formed by a fragment of the mainspring of a watch, ⅜ths of
an inch long, say, is attached to the back of a little circular mirror, made
of extremely thin silvered glass, also about ⅜ths of an inch in diameter. The
mirror and magnet are suspended by a single cocoon-fibre, so fine as to be
almost invisible, in the centre of a coil, A, of fine silk-covered copper wire.
In front of the suspended mirror, in the axis of the coil, is placed a lens of
about four feet focal distance, and opposite to this is a screen having a
571slit, B, in the centre, behind which is placed a paraffin lamp, D. The screen
is provided with a paper scale, C, divided into equal parts, and is placed at
the distance of about two feet from the little mirror. It follows, from this
arrangement, that when the light passing through the slit falls upon the
mirror, it is reflected again through the lens, and an image of the slit is
seen on the scale. This image is immediately above the slit when the beam
falls perpendicularly upon the mirror, and this condition may be brought
about by properly placing the apparatus with regard to the magnetic meridian.
The directive power of the earth over the little suspended magnet
is, however, almost annulled by properly fixing the steel magnet, E, which
slides upon the upright rod, so that the suspended magnet is thus free to
obey the least force impressed upon it by a current passing through the
coil. And when the mirror is deflected through a certain angle, the image
on the scale will be deflected to twice that angle, and thus the smallest
movements of the suspended magnet are readily recognized; not only by
reason of the length of the beam of light, which forms a weightless index,
but because they are doubled by this increased angular deflection.
Fig. 292.—The Mirror Galvanometer.
When the signals are being rapidly transmitted through a long submarine
line, the currents at the receiving station are much enfeebled and
retarded, and the result is that the movements of a suspended needle have
by no means the decided character which is seen in the instruments connected
with land lines. The signals through a submarine cable could not
therefore be received by any apparatus which required a certain strength
of current; but the mirror galvanometer indicates every change in the
currents, and the apparently irregular motions of the spot of light can be
interpreted by a skilled clerk, who, by long experience, recognizes, in quite
dissimilar effects, the same signal sent by the clerk at the other end in
precisely the same way. Thus a first contact, corresponding with a dot of
the Morse alphabet, may cause the light to move some distance on the
scale, a second contact immediately succeeding moves it but a little way
farther, and a third may occasion a movement hardly perceptible.
The messages sent by the mirror galvanometer must be read as they
are received; and, as a telegraphic instrument, it is wanting in the manifest
advantages attending a recording instrument. Sir W. Thomson has,
however, devised another receiving instrument of great delicacy, which is
termed the syphon recorder. We cannot here describe its admirable mechanical
572and electrical details, but the chief feature is that the attractions
and repulsions of the currents are made to produce oscillations in a syphon
formed of an extremely fine glass tube, the shorter branch of which dips in
a trough of ink, and the longer branch terminates opposite to, but not
touching, a band of paper, which is continuously and regularly drawn along
by clockwork while the message is being received. The tube is a mere
hair-like hollow filament of glass, and the ink, which would not itself flow
from a tube of so fine a bore, is squirted out by electrical repulsion when
the insulated reservoir in which it is contained is electrified at the receiving
station by an ordinary machine. The message as written by this instrument
appears thus:
The reader, on comparing these signals with the Morse code on page
560, will have no difficulty in discovering their relation to it.
It now remains to give some account of the line, that is, the conductor
by which the sending and receiving instruments are united, and along
which the currents flow. Overhead lines are nearly always constructed
with iron wires, which are usually ⅙ in. in diameter, and are coated with
some substance to protect them from oxidation. Zinc is often used for this
purpose, the wire being drawn through melted zinc, by which it becomes
covered with a film of this metal—a process known as “galvanizing” iron.
Another mode is to cover the wires with tar, or to varnish them from time
to time with boiled linseed oil, and this must be done in populous places,
where the gases in the air are liable to act upon the zinc. Sometimes underground
wires are used, and these are often made of copper, covered with
gutta-percha, and are laid in wooden troughs, or in iron pipes. They are
protected by having tape or other material, saturated with tar or bitumen,
wound round them. The poles employed to suspend the overhead wires
are generally made of larch or fir, of such a length that when securely
fixed in the ground they rise 12 ft. to 25 ft. above it, and at the top have a
diameter of about 5 in. About thirty poles are required for each mile, and
every tenth pole forms a “stretching-post,” being made stronger than the
others and provided with some appliance by which the wires can be tightened
when required. The wires are attached to the posts by insulating
supports; but at every pole there is always some “leakage,” the amount of
which depends on the form, material, and condition of the insulators.
Glass is quite unsuitable, because its surface strongly attracts moisture,
which thus forms a conducting film. All things considered, porcelain is
found to be the best insulating material for this purpose, since moisture is
not readily deposited on its surface, and even rain runs off without wetting
it; and it is durable, strong, and clean. Fig. 293 shows a telegraph post,
with brown salt-glazed stoneware insulators, shaped like hour-glasses, with
573a perspective view and section of one of them. Another form of insulator,
shown in Fig. 294, has a stalk or hook of porcelain, with a notch, into which
the wire is simply lifted, and is protected above by a porcelain bell. This
form, or some modification of it, is that most generally used.
Fig. 293.—Telegraph Post and Insulators.
Fig. 294.
It need hardly be remarked that only a single wire is required with most
of the modern instruments for communication between any two places.
Each of the many wires often seen attached to the telegraph posts along a
574road or railway represents a distinct line of communication—that is, one
wire may connect the two termini, another may join an intermediate station
and a terminus, a third may belong to two intermediate stations, and so on.
We have already alluded to the discovery by Steinheil of the apparent conducting
power of the earth; and if we must continue to think of complete
circuits, we must regard the earth as replacing for telegraphic purposes the
second or return wire, which was at first supposed essential. For instance,
when a battery current had to be sent from Station A, Fig. 295, which we
may suppose to be London, to Station B, which we may call Slough, it was
at first thought requisite to provide a wire for the return of the current after
it had traversed the coils at the receiving station. But now the connections
are made as shown in Fig. 296, where the return wire is dispensed with,
except a small portion at each end, which is connected with a large plate
of copper buried in the earth; the arrows show the direction of the current,
according to the commonly received notion. By this plan the current
is increased in intensity, for the “earth circuit” appears to offer less
resistance than the copper wire. The view, however, which regards the
earth not as a conductor in the same sense as the wire, but as the great
reservoir or storehouse of electricity, accords better with known facts.
Fig. 295.—Wire Circuit.
Fig. 296.—Wire and Earth Circuit.
The spread of telegraph lines, and the extent to which this mode of communication
is used by the public, may be illustrated by a few particulars
regarding the Central Telegraphic Office in London. The management of
all the public telegraph lines in Great Britain is now in the hands of the
Post Office authorities, and the arrangements at the central office in
London are an admirable specimen of administrative organization. The
Central Telegraph Office occupies a very large and handsome building
opposite the General Post Office, St. Martin’s-le-Grand. In one vast
575apartment in this building, containing ranges of tables, in all three-quarters
of a mile long, may be seen upwards of six hundred telegraph instruments,
besides a number of stations for the receipt and transmission of bundles
of messages by pneumatic dispatch. The number of clerks employed in
working the instruments is 1,200, and about three-fourths of these are
females. The wires from each instrument are conducted below the floor
of the apartment to a board where they terminate in binding-screws,
marked with the number of the instrument. The same board has binding-screws,
with battery connections, and others which form the terminals of
the telegraph lines, and thus the requisite connections are readily made.
The batteries are placed in a lower room, which contains about 23,000
cells of Daniell’s construction, formed into nearly 1,000 distinct batteries,
in each of which the number of cells varies according to the length of the
line through which the current has to pass. Thus, the battery which
supplies the currents that are sent through the coils of the instrument at
Edinburgh consists of 60 cells, but one-sixth of that number suffices for
some of the short lines. The instrument almost exclusively used is the
Morse recorder, and Wheatstone’s automatic punching machine and transmitters
are in constant employment. There are also some examples of
other instruments to be seen in operation, such as the Hughes type printing
telegraph, the American sounder, a few A, B, C, dial instruments, and
a solitary specimen of a double-needle instrument. Upwards of 30,000
messages pass through this office each day.
Fig. 297.—Submarine Cable between Dover and Calais.
But the most striking achievements in connection with telegraphy are
the great submarine lines which unite the Old and New Worlds. Morse
and Wheatstone about the same time (1843) independently experimented
with sub-aqueous insulated wires, and their success gave rise to numerous
projects for submarine lines. How far any of these might have been practical
need not here be discussed, but it fortunately happened that some years
after this, the electrical properties of gutta-percha were recognized, and
this material, so admirably adapted for forming the insulating covering of
wires, was taken advantage of by Brett and Co., who obtained the right of
establishing an electric telegraph between France and England, and they
succeeded in laying down the first submarine cable. This cable extended
from Dover to Cape Grisnez near Calais, and the experiment proved successful;
but, unfortunately, the cable was severed within a week by the
sharp rocks on which it rested near the French coast. It proved, however,
the excellent insulating property of the new material, and demonstrated
the possibility of submarine telegraphic communication. Another cable
576was manufactured, in which the gutta-percha core was protected by a covering
of iron wires laid specially on the exterior, and thus combining greater
security with a far larger amount of tenacity. A view and section of this—the
first practically successful submarine cable—are given in Fig. 297 of
the real size. It has four separate copper wires, each insulated with a
covering of gutta-percha, and the whole was spun with tarred hemp into
the form of a rope, and protected with an outer covering of ten of the
thickest iron wires wound spirally upon it. The cable when complete
was 27 miles in length, and each mile weighed 7 tons. This cable was
laid in 1851, and from that time it has been in constant use, with the exception
of a few interruptions from accidental ruptures. Its success immediately
led to the construction of other cables connecting England with
Ireland, Belgium, Holland, &c. In 1855 the practicability of an Atlantic
cable was no longer doubted, and £350,000 were soon subscribed by the
public for the project. A cable was manufactured weighing 10 tons to the
mile, and in August, 1857, 338 miles of it had been successfully paid out by the
ships when the cable parted. Better paying-out apparatus was now devised—self-releasing
brakes were constructed, so that the cable should not be exposed
to too great a strain; and in 1858 another cable, requiring a strain
of 3 tons to break it, was manufactured, and the laying of it commenced
in mid-ocean—the Mægera and Agamemnon going in opposite directions,
and paying out as they proceeded. Twice the cable was severed, twice
the ships met and repaired the injury; but the third time, when they were
200 miles apart, the cable again broke. But again the attempt was repeated,
and this time success crowned the effort; for on the 5th of August the two
continents were telegraphically connected. Unfortunately the electric continuity
failed after the cable had been a month in use.
Seven years elapsed before another endeavour was made; but the
experience gained in the unsuccessful attempt was not lost; and in 1865
another cable had been constructed, and the Great Eastern was employed
in laying it. In this the conductor was composed of seven copper
wires twisted into one strand, covered with several layers of insulating
material, and covered externally with eleven stout iron wires, each of which
was itself protected by a covering of hemp and tar. This cable was 2,600
miles long, and contained 25,000 miles of copper wire, 35,000 miles of iron
wire, and 400,000 miles of hempen strands, or more than sufficient to go
twenty-four times round the world. It was carefully made, mile by mile,
formed into lengths of 800 miles, and shipped on board the Great Eastern
in enormous iron tanks, which weighed, with their contents, more than
5,800 tons. This cable was manufactured by Messrs. Glass and Elliot,
at Greenwich, to whom the iron wire for the outer covering was furnished
by Messrs. Webster and Horsfall, of Birmingham. Fig. 298 represents
the workshops with the iron wire in process of making. The great ship
sailed from Valentia on the 23rd of July, 1865, and the paying out commenced.
Constant communication was kept up with the shore, and signals
exchanged with the instrument-room at Valentia, which is represented in
Fig. 299, where, among various instruments invented by Sir W. Thompson,
may be seen his mirror galvanometer. After several mishaps, which required
the cable to be raised for repairs after it had been laid in deep
water, the Great Eastern had paid out about 1,186 miles of cable, and was
1,062 miles from Valentia, when a loss of insulation in the cable was discovered
by the electricians on board. This indicated some defect in the
portion paid out, and the usual work of raising up again had to be once
577more resorted to. During this process the cable parted, and Fig. 300
shows the scene on board the Great Eastern produced by this occurrence,
as represented by an artist of the “Illustrated London News” who accompanied
the expedition. The broken cable was caught several times by
grapnels, and raised a mile or more from the bottom, but the tackle proved
578unable to resist the strain, and four times it broke; and after the spot had
been marked by buoys, the Great Eastern steamed home to announce the
failure of the great enterprise. For this 5,500 miles of cable had altogether
been made, and 4,000 miles of it lay uselessly at the bottom of the ocean,
after a million and a quarter sterling had been swallowed up in these
attempts.
Fig. 298.—Making Wires for Atlantic Telegraph Cable.
Fig. 299.—The Instrument-Room at Valentia.
But these disasters did not crush the hopes of the promoters of the great
enterprise, and in the following year the Great Eastern again sailed with
a new cable, the construction of which is shown of the actual size, in
Fig. 301. In this there is a strand of seven twisted copper wires, as before,
forming the electric conductor; round this are four coatings of gutta-percha;
and surrounding these is a layer of jute, which is protected by ten iron
wires (No 10, B.W.G) of Webster and Horsfall’s homogeneous metal,
twisted spirally about the cable; and each wire is enveloped in spiral
strands of Manilla hemp. The Great Eastern sailed on the 13th of July,
and on the 28th the American end of the cable was spliced to the shore
section in Newfoundland, and the two continents were again electrically
connected. They have since been even more so, for the cable of 1865 was
eventually fished up, and its electrical condition was found to be improved
rather than injured by its sojourn at the bottom of the Atlantic. It was
spliced to a new length of cable, which was successfully laid by the Great
Eastern, and was soon joined to a Newfoundland shore cable. There
were now two cables connecting England and America, and one connecting
America and France has since been laid. At the present time upwards
of 20,000 miles of submerged wires are in constant use in various
parts of the world.
Fig. 300.—The Breaking of the Cable.
Certain interesting phenomena have been observed in connection with
submarine cables, and some of the notions which were formerly entertained
579as to the speed of electricity have been abandoned, for it has been ascertained
that electricity cannot properly be said to have a velocity, since the
same quantity of electricity can be made to traverse the same distance with
extremely different speeds. No effect can be perceived in the most delicate
instruments in Newfoundland for one-fifth of a second after contact
has been made at Valentia; after the lapse of another fifth of a second the
received current has attained about seven per cent. of its greatest permanent
strength, and in three seconds will have reached it. During the
whole of this time the current is flowing into the cable at Valentia with its
maximum intensity. Fig. 302 expresses these facts by a mode of representation
which is extremely convenient. Along the line O X the regular
intervals of time in tenths of seconds are marked, commencing from O, and
the intensity of the current at each instant is expressed by the length of
the upright line which can be drawn between O X and the curve. The curve
therefore exhibits to the eye the state of the current throughout the whole
time. If after nearly a second’s contact with the battery the cable be connected
with the earth at the distant end, the rising intensity of the current
will be checked and then immediately begin to decline somewhat more
gradually than it rose, as indicated by the descending branch of the curve
in Fig. 302. A little reflection will show the unsuitability for such currents of
580instruments which require a fixed strength to work them. We may remark
that, supposing a receiving instrument were in connection with the Atlantic
Cable which required the maximum strength of the received current to
work it, the sending clerk would have to maintain contact for three seconds
before this intensity would be reached, and then, after putting the cable to
earth, he would have to wait some seconds before the current had flowed
out. Several seconds would, therefore, be taken up in the transmission of
one signal, whereas by means of the mirror galvanometer about one-fourteenth
of this time suffices, and the syphon recorder will write the messages
twelve times as fast as the Morse instrument. The cause of the gradual
rise of the current at the distant end of a submarine cable must be sought
for in the fact that the coated wire plays the part of a Leyden jar, and the
electricity which pours into it is partly held by an inductive action in the
surrounding water. The importance of Sir W. Thomson’s inventions as
581regards rapidity of signalling, upon which the commercial success of the
Atlantic Cable greatly depends, will now be understood.
Fig. 301.—Atlantic Telegraph Cable, 1866.
Fig. 302.
By furnishing the means of almost instantaneous communication between
distant places, the electric telegraph has enabled feats to be performed
which appear strangely paradoxical when expressed in ordinary
language. When it is mentioned as a sober fact that intelligence of an
event may actually reach a place before the time of its occurrence, a very
extraordinary and startling statement appears to be made, on account of
the ambiguous sense of the word time. Thus it appears very marvellous
that details of events which may happen in England in 1876 can be known
in America in 1875, but it is certainly true; for, on account of the difference
of longitude between London and New York, the hour of the day at the
latter place is about six hours behind the time at the former. It might,
therefore, well happen that an event occurring in London on the morning
of the 1st of January, 1876, might be discussed in New York on the night
of the 31st of December, 1875. There are on record many wonderful instances
of the celerity with which, thanks to electricity, important speeches
delivered at a distant place are placed before the public by the newspapers.
And there are stories in circulation concerning incidents of a more romantic
character in connection with the telegraph. The American journals
not long ago reported that a wealthy Boston merchant, having urged his
daughter to marry an unwelcome suitor, the young lady resolved upon at
once uniting herself to the man of her choice, who was then in New York,
en route for England. The electric wires were put in requisition; she took
her place in the telegraph office in Boston, and he in the office in New
York, each accompanied by a magistrate; consent was exchanged by
electric currents, and the pair were married by telegraph! It is said that
the merchant threatened to dispute the validity of the marriage, but he did
not carry this threat into execution. The following jeu d’esprit appeared
a short time ago in “Nature,” and, we strongly suspect, has been penned
by the same hand as the lines quoted from “Blackwood,” on page 508.
ELECTRIC VALENTINE.
(Telegraph Clerk ♂ to Telegraph Clerk ♀.)
“‘The tendrils of my soul are twined
With thine, though many a mile apart;
And thine in close-coiled circuits wind
Around the magnet of my heart.
“‘Constant as Daniell, strong as Grove;
Seething through all its depths like Smee;
My heart pours forth its tide of love,
And all its circuits close in thee.
“‘Oh tell me, when along the line
From my full heart the message flows,
What currents are induced in thine?
One click from thee will end my woes!’
“Through many an Ohm the Weber flew,
And clicked this answer back to me—
‘I am thy Farad, staunch and true,
Charged to a Volt with love for thee.’”
[Note by the Editor.—Ohm, standard of electric resistance; Weber, electric current; Volt, electro-motive force; Farad, capacity (of a condenser).]
Of more recent invention than any of the classes of instruments
already mentioned for electrical communication at a distance is the
telephone, which differs widely from the rest in many notable particulars.
Though the telephone completely realized what had for years before been
the dream of physicists, the first announcement of its capabilities was
received, even by the scientific world, with some pause of incredulity; but
582when its powers were demonstrated, it created no small sensation. It
has now, within a few years afterwards, become so familiar as an appliance
of ordinary life and business, that people in general are less impressed by
the wonder of it than were their fathers half a century ago by the electric
telegraphs of Wheatstone and of Morse. Like all other inventions, it
was led up to by preceding discoveries and tentative efforts. It will be
unnecessary here to trace those successive steps with minuteness, or to
attempt to adjust the claims of merit or priority that have been put
forward for different inventors, but a notice of some of the stages in the
evolution of this wonderful contrivance may be of interest. If the reader
has no previous knowledge of the physical nature of sounds in relation to
music, and especially to articulate speech, he should now refer to the brief
explanation given in a subsequent chapter, at the commencement of the
section on the Phonograph. He should, however, bear in mind that in
that explanation are included some acoustical discoveries of a later date
than some of the inventions we are here to speak of, or, at least, the real
causes of which give other qualities than pitch to sound, had not been
fully demonstrated when the notion of the electric telephone was conceived.
When the electric telegraph came into use and it was found possible to
use it for communication of intelligence to great distances, it is not
surprising that the further problem of transmitting by electricity, not
signals merely, but audible speech, should be suggested. Perhaps the
first scientific person who avowed a belief in the possibility of doing this,
and even indicated the direction in which the solution of the problem was
to be sought, was a Frenchman of science, M. Charles Bourseul. In 1854,
he pointed out that sounds are caused by vibrations, and reach the ear by
like vibrations of the intervening medium, and, although he could not say
what took place in the modifications of the organs of speech by which
syllables are produced, he inferred that these syllables could reach the ear
only by vibrations of the medium, and that if these vibrations could be
reproduced the syllables would be reproduced. He suggests that a man
might speak near a flexible disc, which the vibrations of his voice would
throw into oscillatory movements that could be caused to make and break
a battery circuit, and that, at a distance, the currents might be arranged
to produce the like vibrations in another disc. The weak point of this
scheme was the want of any suggestion as to the mode in which this last
effect was to be produced. Even when this part of the problem was
solved in a few years afterwards, as we shall presently see, it was musical—and
not articulate—sound that could be transmitted by an arrangement,
using make and break contacts. The reader, who has understood what
has been said of electrical currents, and also the account of the compounded
vibrations in articulate sounds introduced into our section on the
phonograph, should have little difficulty in seeing this must necessarily be
the case, for the contacts could only give the succession of the vibrations
by currents of equal intensity, and could not, like the yielding wax of the
phonograph cylinder, correspond with their relative intensities. M. Bourseul
pointed out advantages which would arise from the transmission of
speech by electricity, such as simplicity of apparatus and facility in use—for,
unlike the telegraph, no skilled operators would be needed—to
signal messages, or time spent in spelling out the words letter by letter.
He says that he had made some experiments, which promised a favourable
result, but demanded time and patience, and that he is certain that,
583in a more or less distant future, speech will be transmitted by electricity,
so that what is spoken in Vienna may be heard in Paris. One cannot
help thinking that if M. Bourseul had but pursued his experiments a little
longer, he would not improbably have achieved the invention of the
speaking telephone, for which the world had to wait twenty years longer.
As it is, we cannot but admire his scientific foresight and his confidence
in the ultimate realization of his idea.
But before this came to pass, an intermediate stage was reached in the
apparatus contrived by M. Reiss, a schoolmaster of Friedrichsdorf, who,
in 1860, solved the problem of electrically transmitting musical tones. So
far as concerned the reproduction of the sounds, this telephone was founded
upon a discovery, made in 1837, by an American physicist, named Page,
which was this: At the moment a bar of iron is magnetized, by sending a
current through a coil surrounding it, as shown in Fig. 265, a slight but
sharp click is heard. The transmitting apparatus was, in principle,
Mr. Scott’s phono-autograph (described in the section on the phonograph),
which had been invented in 1855. The tracing style of this was replaced
in Reiss’ apparatus by a small disc of platinum, connected by a very light
spring of the same metal with a binding-screw for the battery connection.
Nearly in contact with the little disc was a platinum point, so arranged
that the slightest oscillation of the membrane would bring them into
actual contact and thus close the circuit. Worthy of remark is the very
primitive nature of the materials with which Reiss made his first experimental
apparatus. The receptacle for the voice was simply a large bung
hollowed out into a conical cavity, and the membrane was supplied by the
skin of a German sausage, while the clicking bar of the receiver was a
stout knitting needle, surrounded by a coil of covered copper wire and
stuck into the bridge of a violin, which, by acting as a sounding board,
made the clicks produced in the needle distinctly audible. M. Reiss
finally produced his telephone in the form shown in Fig. 302a, where I is
the receiver; B, the voltaic battery; I I, the receiver; c c is a coil of insulated
wire, surrounding a slender iron rod, mounted on the supports, f f,
which rest on the sounding board, g g. The transmitter consists of the
hollow box, A, provided with a trumpet-mouthed opening in one side and
having at the top a circular piece cut out, across which is stretched a membrane
with the little disc of platinum, n, fixed in its centre. When a person
applying his mouth to A sings into the box, the membrane is thrown into
vibrations corresponding with the notes, and at each vibration a contact
is made and a click is emitted from the distant sounding box. The tones
are concentrated by covering this box with the perforated lid. It was
afterwards found that a trumpet mouth fitted into the receiver was still
more effective. Reiss tried to use his arrangement for transmitting
speech, but without success, although occasionally a syllable could be
very indistinctly heard. An instrument, with springs so nicely adjusted
that slight vibrations did not separate the platinum from actual contact,
but merely caused change of pressure, has indeed been made to convey
articulate sounds, although the arrangement was not essentially different
from that of M. Reiss. This mode of action is, however, a different thing,
and we shall presently see that very effective speech transmitters have
been constructed by applying it in a more refined way. This musical
telephone could give the pitch of the sounds in the song but not their
quality (timbre), and the receiver added to the main system of vibration
other sets that belonged to itself, the result being a shrill and by no
584means pleasing tone, recalling that of a penny trumpet. Messrs. C. and L.
Wray afterwards effected some considerable improvements in M. Reiss’s
telephone, with the object of intensifying the effects and producing better
tones.
Fig. 302a.—Reiss’ Musical Telephone.
Fig. 302b.—Bell’s Musical Telephone.
A further step towards the speaking telephone may be illustrated by
an earlier invention of Mr. Graham Bell, a native of Scotland, who had
settled in the United States. Mr. Bell’s inventions, it may be mentioned,
were by no means the results of fortunate accidents or of unsought
and spontaneous flashes of conception, but rather the outcome of long,
patient and systematic studies. His father, Mr. Alexander Melville Bell,
of Edinburgh, had assiduously cultivated acoustic science, and had in
585conjunction with his son, undertaken special researches into the mechanism
of the organs of speech, the elements of articulate speech in different
languages, and the musical components of vocal sounds. When Graham
afterwards pursued these studies in the light of the fuller investigation
carried out by Helmholtz, he was naturally led to the application of
electricity to acoustic transmission. After some experiments in the
production of vowel sounds by combinations of electric tuning forks, he
invented a telephone for reproducing musical sounds at a distance, which
was a great improvement on that of Reiss, and involved another principle,
which indeed is the same as that utilized in his more mature invention of
the speaking telephone. As a like explanation of the action would apply
in both cases, the reader will find his advantage in following the observations
we have to make on the earlier instrument. This consisted of what
was virtually two sets of electric tuning forks, each set being acted upon
by one electro-magnet. Fig. 302b will suffice to show the general form of
the arrangement. A plate of steel is bent twice at right angles longitudinally,
and is magnetized so that any transverse slice of it would
constitute an ordinary horse shoe magnet. This is seen endways in
Fig. 302b at M, and N. and S. will indicate the north and south poles
respectively. To each limb of this broad magnet is attached a plate of
586steel, T, cut into teeth, just in the same way as the steel plate in a common
musical box or mechanical piano, except that the teeth are not pointed.
These are tuned to give severally in pairs the notes of the musical scale
when thrown into vibration. Between the prongs of the series of tuning
forks thus formed is an electro-magnet, L, made of a bar of soft iron, I,
wound longitudinally by a coil, one end of which makes an earth connection
at E and the other is connected by the wire, W W´, to complete the
circuit through the coil of the distant apparatus. It will be observed that
the receiving and transmitting instruments are exactly alike. Now, suppose
one of these teeth is struck or otherwise thrown into vibration, the
result will be, since the free ends of the teeth are magnetic poles, that alternating
electric currents will be generated in the coil of the electro-magnet
(see page 509), and these will flow through the entire circuit, including the
coil of the distant instrument, where the magnetism generated will alternately
attract and repel the polar extremities of the teeth in the steel
plate. It will be understood, of course, that the fellow prong of the fork
will vibrate also, and will simultaneously approach to and recede from the
soft iron core, so that being of opposite polarity, the effect on the electro-magnet
will be doubled. The action on the distant electro-magnet will
be a rapid series of reversals of the polarities of the core, and hundreds of
times in every second the ends of the steel teeth will be alternately
attracted and repelled. But not all of these will thereby be thrown into
vibration—only the one pair which were tuned into unison with the former
can and will respond to that particular series of impulses, and the consequence
will be that the same note will be emitted by the receiving instrument.
If two or more notes of the transmitter be simultaneously thrown
into vibration, the same notes will be heard from the receiver, for each
series of currents will flow along the wire independently, just as if the other
did not exist, and each will produce its particular effect on the transmitter.
In this way an air played on the one instrument is heard also from the
other, with all its accents and combinations. But more than this, if a
tune be played on a musical instrument near the sender, or if a song be
sung, the air will be reproduced by the distant receiver. The reason of
this is that the steel tongues take up, or are thrown into movement by,
the vibrations that have the same periodicity. The manner in which a
vibratory body responds to impulses of its own periodicity may be easily
shown by exposing the wires of a piano and raising the dampers, when, if
a note be sung near the instrument, it will be found that a number of the
wires respond, namely, those that are capable of vibrating synchronously
with the constituent vibrations of the voice, for neither a voice nor a
sounding wire gives forth one simple system of vibrations, the audible
effect being due to the superposition or composition of several diverse
elementary systems. With the same arrangement another experiment
may be made, as an illustration of a matter important for our subject.
Let the different vowels be sung to the piano-wire on the same note or
pitch, and in the responses to each a difference of the quality of the
sound will be noticed, although the piano will not distinctly give back the
vowel itself. It would, however, do so if a number of its wires were
strung with certain definite relations in pitch to that of the fundamental
note and in unison with the voice components of the vowel sound.
Fig. 302c.—Superposition of Currents.
It has been said above that two systems of electrical currents of
different periodicity would flow along one wire independently of each
other, but it should be explained that this takes place by a composition of
587the currents, for it is evident that at any given instant the wire can only
be in one of three conditions, viz.: (1) with no current flowing; (2) with a
current in the positive direction; (3) with a current in the negative direction.
Such must always be the case, and, therefore, it should be clearly
understood how this is consistent with the superposition of currents of
different periodicities, a matter which the diagram, Fig. 302c, is intended
to illustrate. Suppose the flow of time to be represented by the dotted
lines from a to b, the whole length of which we may call 1 100th of a
second, and that the current passing through the wire is represented in
intensity and direction by the plain lines; the intensity by distance above
or below the dotted line; the direction being positive where the plain
line is above, and negative when it is below the dotted straight line, and
of course no current at all occurs at the instant when the change of direction
takes place. The line A will thus represent alternating currents,
rising and sinking in intensity, and changing from one direction to the
other, going through 600 regularly recurring phases in one second of
time. Similarly, B may represent another series of currents, having here
a periodicity of 500 in one second of time. These are here supposed to
have greater intensity than the former. If the two currents are sent
through one wire their effects are superposed, so that the actual electrical
state of the wire would be represented by the curve C, which is compounded
from the two others, and where it will be observed the rise and
fall of the current, its maxima and minima, no longer recur at regular
intervals within the space of the 1 100th of the second, the whole of that
period being taken up by a less regular series of changes, the cycle being
repeated only 100 times in the second. The same diagram might serve
to illustrate the motions of, say, a particle of air or the drum of the ear in
acoustic vibration, the distances above and below the straight line being
taken to represent the displacements from the position of rest on one side
and the other. If the sounds of an organ or piano consisted of only these
primary vibrations, B would roughly[8] represent the movements of the
588wires, the air and the drum of the ear, when the
note si3 was sounded alone; A when the note
re4 was more faintly sounded alone, and then C,
if these notes were sounded together, would correspond
with the movements of the drum of the
ear. The movements it actually makes when we
hear speech, or even a single musical note, are,
however, a thousand-fold more complex, for no musical instrument gives
out a note with a single set of vibrations, the fundamental one being always
accompanied by other sets diversely related to it, according to the class of
instrument. In some cases, fifteen or sixteen sets of vibrations have been
distinguished along with the fundamental note, without exhausting the
possible number. Of a like order of complexity will be the currents
which the wire of a speaking telephone must convey, and the difference
between the undulatory nature of the currents in Bell’s musical telephone
and any produced by mere make and break contacts, as in Reiss’ arrangement,
will be obvious, and recognized as an important step towards the
solution of the problem of transmitting speech. When Mr. Bell invented
his instrument, he was seeking for a method of simultaneously transmitting
by one wire several messages by audible signs merely; and by the
method used in his musical telephone this is practicable, for all that
would be required
would be pairs of
transmitters and
receivers, each adjusted
to one single
particular note.
Another point that
should be noted is
that in the Bell
musical telephone
no battery is used,
for the currents are
those generated by
magneto-electric
induction, and the circuit through the wires and coils are completed by
earth connections.
8. The lines A and B in the diagram have not harmonic ordinates.
Fig. 302d.—Bell’s Speaking Telephone.
In passing from the invention of the musical to that of the speaking
telephone, Mr. Bell passed from the more complex to the more simple
instrument, for of all apparatus by which communication can be carried
on at a distance, the Bell speaking telephone is one of the simplest. He
had only to make its vibrating disc of Scott’s phono-autograph into a magnetized
body, capable of producing currents in an electro-magnet coil in
the same way as did the vibrating plates in his musical telephone. The
Bell speaking telephone was publicly exhibited for the first time at Philadelphia,
in 1876, and was shown the same year to the British Association
by Sir William Thomson, who pronounced it the wonder of wonders.
For the first time in England, the instrument in a still simpler form was
exhibited by Mr. Preece, at the Plymouth meeting of the British Association
in 1877, and of nearly the same construction as is still often used,
although, as we shall presently see, for battery telephones the
transmitting apparatus is now made of larger dimensions, of a different
shape and on a different principle. We shall describe the simple form in
589which transmitter and receiver are identical, each consisting externally of
a small cylindrical wooden or ebonite box, and with a handle three or four
inches in length of the same material. Fig. 302d is a section of the instrument
where N S is a cylindrical steel magnet, on one end of which is
wound the small coil B, made of fine silk covered copper wire, the extremities
of which pass through the handle M at f f, and are connected by the
binding screws I I´ with the line wire C C´. Close to the coil covered
end of the magnet is a very thin diaphragm of iron, L L´, and when this is
thrown into vibration by the voice speaking into the trumpet-mouth
opening, R R´, its movements produce currents in the coil according to the
principles that have already been explained, for it will be observed that
the iron disc is magnetized by the inductive action of the permanent
magnet N S. These currents passing through the coil of the receiving
instrument raise or lower the intensity of the magnetic force in it, so that
the distant disc reproduces the vibrations of the transmitter. Such is at
least an obvious explanation of the action of this very simple arrangement;
but from a number of experiments and observations that have been
made with modifications of the instruments, it would appear that other
and much more complex phenomena concur in producing the effects. It
has indeed been suggested—and the idea is supported by numerous experiments—that,
in these telephonic transmissions of speech, vibrations are
concerned which are not at all of the mechanical kind we have been dealing
with in these explanations, but are molecular.
The Bell telephone is used by speaking distinctly before the mouth-piece
of the transmitter, while the listener at the other end of the line
applies the mouth-piece of his instrument to his ear, and one wire is
sufficient with good earth connections, although sometimes a second wire
is employed to complete the circuit. It is also found advantageous to
have two instruments in the circuit at each end, so that one may be held
to the ear while the operator is speaking through the other. In this way,
a rapid conversation can be carried on with the greatest ease, or again, an
instrument may be held at each ear, by which arrangement the words are
more distinctly heard. It is not necessary to shout, as this has no effect,
but to speak with a clear intonation, and some voices are found to suit
better than others. The vowel sounds are best transmitted, except that
of the English e, which, with the letters g, j, k, and q, are always somewhat
imperfectly transmitted. A song is very distinctly heard, both in the
words and the air, and the voice of the person singing is readily recognized.
Several instruments may be included in one circuit at different stations, so
that half a dozen persons may take part in a conversation, and questions
and answers may be understood even when crossing each other. If two
distinct telephone circuits have their wires laid for a certain distance
(two miles) near each other, say a foot or more apart, and without any
connection whatever, listeners at the end of the one line will hear the conversation
exchanged through the other line. Other forms of the instruments
have been arranged, by which a large audience may hear sounds
produced at a distance, as, for instance, when a cornet-à-piston was played
in London, it was heard by thousands of people assembled in the Corn
Exchange at Basingstoke.
It would be impossible within our limits to even briefly describe the
great number of improvements and modifications of Bell’s system that
were devised by various persons soon after the invention was brought out,
and many additional complications were introduced into some of the
590arrangements. Advantage was also taken to a greater or less extent of
another principle affecting the strength of electric currents, to which we
have now to call the reader’s attention, and to exemplify by one of the
simplest instruments, leaving detailed accounts of the various forms in
which it has been applied to be found in special treatises. The reader
should first turn back to page 400, where he will see an expression of the
strength of a battery current. It will be observed that the current may
be increased or diminished by diminishing or increasing R, the external
resistance, without changing the other terms. Now M. Du Moncel discovered,
as far back as 1856, that an increase of pressure between two
conductors in contact, and conveying a current, caused a diminution of the
electrical resistance, and this discovery was utilized for telephonic purposes
by Mr. Edison in his invention of the carbon transmitter (1876). In this
there is no magnet, and a stretched membrane may take the place of the
metallic plate, although a circle of photographers’ ferro-type plate gives
better results. A pad of india-rubber, cork, or other material is fixed on the
plate, and rests upon a carbon disc, which again is in contact with a metallic
conductor. Between the latter and the carbon the current from a
constant battery passes. When the plate is thrown into vibration by
speaking into the mouth-piece, the variations of pressure conveyed to the
carbon cause variations in the resistance of its electrical contact, and thus
a series of undulations are produced in the current, and these affect the
electro-magnet of a Bell receiving instrument in the circuit as before, so
that the sounds are reproduced. It is now time to say a word about the
share in the invention of the speaking telephone which has been claimed
by Mr. Elisha Gray, also of the United States, who, at the time Mr. Bell
applied for the patent for his instruments, produced drawings and descriptions
of a plan he had devised for transmitting speech by undulating
electrical currents, and it has been admitted that the plan he had conceived
was perfect in principle. He proposed to use a battery current,
and his receiving instrument was nearly the same as Bell’s. The undulations
of the current were also determined, as in Edison’s telephone, by
changes in the external resistance, but this was effected in a different,
though equally simple manner. To a membrane stretched across the
lower end of a short wide tube that formed the mouth-piece of the transmitter,
and was placed vertically, was attached a piece of platinum wire,
conveying the current and dipping into a liquid of moderate conductivity,
but not quite touching another platinum electrode fixed at the bottom of
the vessel containing the liquid. The space of liquid traversed by the
current being thus varied by the oscillations of the membrane, the
resulting variations of the resistance produced the requisite undulations
in the intensity of the current. Both Mr. Bell and Mr. Gray applied for
patents on the 14th February, 1876, but the American Patent Office
recognized the claim of the former as prior.
Fig. 302e.—Mr. Hughes’ Microphone.
(BandRare merely diagrammatic.)
Du Moncel’s observation was applied by Mr. Hughes in the construction
of an instrument, which he named the microphone. This was in the
same year that Edison had brought out his carbon telephone, and a
certain similarity, resulting from the identity of the principle employed,
led to an acrimonious controversy on what were supposed to be rival
claims. But the microphone differs so much in arrangement and performance
from the other instrument as to constitute a distinct invention.
The instrument, if it may be so called, is simplicity itself, in the form
represented in Fig. 302e, which is one of the most sensitive. There,
591C and C´ are two small blocks of carbon, fixed on a small upright piece of
wood. Two cup shaped cavities are hollowed out in the carbon blocks,
and these serve to hold loosely, in a nearly vertical position, a small rod
of gas retort carbon pointed at the ends. This rod is only about one inch
in length, and the lower end merely rests on the bottom of the cup in C´,
while the other is capable of moving about in the upper cavity, the vertical
position being nearly maintained in a state of unstable equilibrium. The
carbons are in the circuit of a voltaic cell or small battery, B, in the line
through a Bell receiving instrument, which may be at a distance. When
the microphone is to be used, it is placed on a table with a cushion
or several folds of wadding beneath its base. If the receiver be
applied to the ear of a listener, he will distinctly hear every word pronounced
by one speaking near the microphone, even in a low tone; but a
loud voice may be heard when the speaker is 20 or 30 feet from the
instrument. The minutest vibrations conveyed to the stand are perceived
at the receiver as loud noises. The tread of a fly walking over the board,
S, is heard like the tramp of a horse, and the ticks of a watch are audible
in the receiver when the ear is several inches away from it. The slight
touch of a feather on the stand is distinctly audible, and a current of air
impinging upon it is reproduced as the noise of a stream of water. The
microphone is, in fact, the most sensitive detector of vibrations that is
known, and its employment as a transmitter has brought the telephone to
its present perfection. It has been constructed in an endless variety of
forms, according to the purposes for which it is intended, and its simplicity
is as wonderful as its extreme sensitiveness. We will further illustrate
these qualities by an experiment of Mr. Willoughby Smith’s on the same
principle. Instead of the two carbon blocks, he laid on the table, in
parallel positions, two small rat tail files, and completed the circuit by a
third file, laid across the others at right angles. This arrangement constituted
so sensitive a transmitter that the listener at the distant Bell
receiver could hear even the faint sound of the speaker’s breathing.
Even three common pins, similarly crossed, make an effective transmitter.
The feebleness of the variations in the current requisite to make the Bell
592receiver produce sounds is extraordinary, and a very weak battery current
is sufficient, even under the circumstances of ordinary practical use.
Still more remarkable is the fact that in favourable conditions the microphone
is capable of transmitting sound without any battery at all, but
merely with connections to earth, when the ticking of a watch placed upon
the stand has been distinctly heard at the distance of nearly one-third of
a mile, and speech, also, has been transmitted with unusual distinctness
with the battery left out and merely a few drops of water placed at the
carbon contacts; indeed, it is said that, even without the water, the
voice may be heard. This effect has been attributed to the carbons
and water forming a battery themselves, and in the latter to the moisture
of the speaker’s breath supplying the fluid element. But, again, the
microphone will not only transmit speech, but, under certain arrangements,
it will reproduce it (when one of the carbon electrodes is
attached to a membrane), although the result is less distinct than
with the Bell receiver. It is, however, not so easy to explain how mere
variations of current intensity can produce the effect where there can
be no magnetic attractions and repulsions. We must, no doubt, look
for the cause in some other property of electric currents. The transmitters
used in various lines of telephonic communication, erected by the
Post Office or by companies in Great Britain, are generally applications
of the principle of the microphone, and not of that of either Mr. Bell’s or
Mr. Edison’s original instrument. But more recently, Mr. Edison has
most ingeniously adapted variations of sliding friction, as modified by the
action of the undulatory current on a liquid electrolyte between the sliding
surfaces to the production of a loud speaking telephonic receiver—that is,
one by which the sounds are made audible to a large assembly. From this
instrument, the notes of a cornet-à-piston, played in Brighton, have been
distinctly heard throughout a large hall in London.
Another curious transmitter is formed of a fine jet of water traversed by
an electric current. Acoustic vibrations are easily set up in the jet, and
these modify its conductivity so as to produce corresponding undulations
of current intensity.
It would take long to point out the many scientific applications of so
sensitive an instrument as the microphone with its Bell receiver. As a
medium for conveying speech to a distance, whether for purposes of peace
or war, its use is sufficiently obvious. Some curiosities of musical transmission
have been noticed, and such experiments are repeated from time
to time with increasing success. It has been applied to many purposes in
surgery and medicine. In many cases of deafness it has made conversation
easy. Even the passage of the molecules of gases, when diffusing
through porous partitions, Mr. Chandler Roberts has by its means made
audible. The distances to which speech can now be transmitted are
considerable, as conversations have been carried on by persons nearly
300 miles apart.
593
LIGHTHOUSES.
Who does not regard with interest the lighthouses which at night throw
their friendly beams across the sea, to guide the mariner in his course,
and warn him of perils from sunken rock or treacherous shoal? The
modern lighthouse, with its beautiful appliances, is entirely the result of
the applied science of our age; and it affords a fine example of the manner
in which experiments, carried on to determine natural laws apparently of
an abstract character and without any obvious direct utility, give rise to
inventions of the highest importance and most extended usefulness. The
lofty structures which were erected near certain ancient harbours, and of
which the Pharos of Alexandria is the most memorable example, burned
on their summits open fires of wood; and whatever beacons existed from
that time down to the end of last century were merely blazing fires of wood
or coal. The lighthouses of the South Foreland, which were established
in 1634, displayed coal fires until 1790, and the lighthouses in the Isle of
Man were first illuminated with oil only in 1816. Down to the beginning
of the present century, therefore, the modern lighthouses showed no improvement
on the ancient plan. Even the Tour de Cordouan, at the mouth
of the Garonne river, which was completed in 1610, and is one of the most
famous of modern lighthouses, from its great height (200 ft.), and the care
which has always been given to render it efficient, showed down to 1780
594merely a fire of billets of wood, the upward loss of the light being diminished
by a rude reflector in the form of an inverted cone. In the improved
means of obtaining artificial light, and in the admirable optical apparatus
by which that light is utilized, we find the vast superiority of modern lighthouses.
But these are sometimes erected on isolated, and almost submerged,
rocks, exposed to the fury of the waves. The difficulties which
have to be overcome in their construction cause some lighthouse towers to
rank among the best specimens of engineering skill. We may, therefore,
consider under the present head—the
towers; the sources of
light; the optical apparatus and
its accessories.
Fig. 303.—The Eddystone Lighthouse.
One of the best-known lighthouses
on the English coast is
that on the Eddystone Rock,
about 14 miles S.S.W. from Plymouth.
The structure which now[9]
stands upon this rock was the
work of Smeaton, and was completed
in 1759. The stones forming
the lower courses of this tower,
which is represented in Fig. 303,
half in section and half in elevation,
are dovetailed into the rock
itself and into each other. The
masonry is carried up in a solid
mass for about 12 ft., the stone
used being granite, which also
constitutes the whole of the exterior
masonry. The four upper
apartments are formed with arched
roofs, the side-thrust of which
is counteracted by iron chains
surrounding the tower. These
chains, which are bedded in lead,
were placed in their positions while hot, and by their contraction bound
the structure together with great force. The masonry of the tower is
68 ft. high, and this is surmounted by the light-room, the total height
from the lowest course of stonework to the gilt ball at the top being 94 ft.,
or nearly half that of the London Monument. The diameter at the base is
26 ft., and that at the top 15 ft. The light-room is of an octagonal shape,
and is made of iron framework, glazed with thick plate glass. Below this
are two store-rooms, a kitchen, and a bed-room. The Eddystone has now
breasted the storms of more than a hundred years, and it remains as firm
as the rock it is built on. Fig. 304 is a picture of this noble lighthouse,
with the British fleet passing close to it, during a furious gale on the 22nd
of October, 1859, or exactly a century after the completion of the structure.
The incident of the man in the water, which occupies the foreground, is not
an imaginary one, for it is recorded that the Trafalgar stopped in the midst
of the storm to pick up a man who had fallen overboard. For eighteen
hours the ships encountered the fury of the tempest, keeping out at sea in
595open order throughout the night. They wore in at dawn, came up the
Channel in line of battle, steamed into Portland, and took up their anchorage
without the loss of a sail, a spar, or a rope-yarn.
9. Smeaton’s tower proving unsafe, has since been taken down and replaced, in 1882, by one
from Mr. Douglass’ design.
Fig. 304.—The Eddystone in a Storm.
The lighthouse tower on the Bell Rock is 100 ft. high, 42 ft. in diameter
at the base, and 15 ft. at the top. The Inchcape Rock, on which it is
placed, is the scene of Southey’s ballad of “Ralph the Rover,” and the
lighthouse here is one of the most serviceable on the Scottish coast, for the
596dangerous spot on which it is placed lies in the direct track of all vessels
entering the Firth of Tay from the German Ocean. The rock is submerged
at spring tides to the depth of 12 ft. The tower bears a close
resemblance in shape to that of the Eddystone: it is circular and faced
with massive blocks of granite. The lower part, to the height of 30 ft., is
solid, and the door is reached by a bronze ladder. The building contains
five apartments, and a cistern for storing fresh water for the use of the
keepers, who have sometimes to remain in their solitary situation for six or
eight weeks together, the weather preventing the possibility of any communication
with the shore.
Still loftier than the tower on the Bell Rock is that which rises in the
midst of the Skerryvore Reef, 12 miles from Tyree, a small island off the
coast of Argyleshire. This building may be taken as a typical specimen of
a detached lighthouse, and the difficulties overcome in its construction
attest the skill of the engineer, Mr. Alan Stevenson, who has written a
highly interesting account of the work. The rocks here are of gneiss, an
extremely hard formation, and their surfaces are worn as smooth as glass
by the action of the water. On one of a numerous series of these small
islets, where only a narrow strip of rock, a few feet wide, remains above
the surface at high water, and this divided by rugged lumps into narrow
gullies, through which the sea constantly rushes, the lighthouse is built. The
work was commenced in 1838 by the erection of a temporary wooden barrack
on piles at a little distance from the site chosen for the foundation. In
a gale during the winter the whole of this structure was swept away in one
night. Another, more strongly secured, was built the following summer,
and in this Mr. Stevenson and his men remained sometimes for fourteen
days together, the weather preventing any passage to or from the shore:
here the men were sometimes awakened from their hard-earned repose by
the water pouring over the roof, and by its rushing through the crevices,
while the erection swayed and reeled on its supports. Mr. Stevenson relates
that one night the men became so alarmed for the stability of their
shelter that some descended, and sought in cold and darkness a firmer
footing on the rocks. Two summers were occupied in cutting the foundations,
and the blasting of the rock in so narrow a space was an operation
attended with no little danger. A small harbour had to be formed at the
rocks for the vessels bringing the ready-prepared stones of the building
from the quarries, where also piers were built expressly for the shipment of
the materials. In designing his tower, the engineer preferred to oppose the
force of the waves by the weight of his structure, rather than to rely on
dovetailed or joggled-jointed stones. Measurements were made of the
force of the waves, which at Skerryvore was sometimes equivalent to a
pressure of 4,335 lbs. on the square foot; and calculations based on these
measurements showed that the mere weight of the superstructure would
amply suffice to keep the stones immovable. Nearly 59,000 cubic feet of
stone were used, or about five times the quantity contained in the Eddystone
Lighthouse, and the total cost of the building was £87,000.
The use of iron, as a building material advantageously replacing stone,
has extended to lighthouses, and many have been constructed entirely of
cast and wrought iron, or partly of iron and partly of gun-metal, which is
not readily acted on by the sea spray. Such lighthouses are cheap, easily
and quickly erected, strong enough to bear shocks and vibrations, and
proof against fire, lightning, and earthquakes. The lighthouse on Morant
Point, Jamaica, is made of iron, cast in England; and it was erected in a
597few months at a cost of one-third of that of a stone tower of the same
altitude. Its height is 105 ft., and the shaft is formed of iron plates in
segments of 10 ft. high, which are bolted together at their flanges. At
Gibbs Hill, Bermuda, is a lighthouse 130 ft. high, constructed in the same
manner.
So inefficient, inconvenient, and uncertain were the lamps or other means
of artificial illumination known up to nearly the beginning of the present
century, that nothing better could be found for the Eddystone Lighthouse
for forty years after its erection than tallow candles stuck in a hoop—a
means of illumination which would scarcely now be tolerated even in a
booth at a village fair. To M. Argand, a Frenchman, we are indebted for
the first great improvement in lamps. The admirable invention which
bears his name is, as everybody knows, an oil lamp with a tubular wick,
which occupies the annular space between two metallic tubes, in such a
manner that a current of air rises through the inner tube, and thus reaches
the interior of the flame. This current, and the current which supplies the
exterior, are increased by surrounding the flame with a tall glass chimney;
and a contraction of the chimney, just above the flame, aids greatly in distributing
the air, so as to insure the complete combustion of the oil. In
the original lamp the supply of oil to the flame depended on the capillary
attraction in the meshes of the wick. M. Carcel applied clockwork to continuously
pump up the oil into the burner, so that, by overflowing, it was
maintained at an invariable level. This arrangement added greatly to the
intensity and steadiness of the light; and, on account of the uniformity of
its flame, the Carcel lamp has been selected as a standard to which, in
France, photometric determinations are referred.
The power of the Argand lamp, as employed in lighthouses, is greatly
increased by the plan of employing several concentric wicks instead of one.
Between these wicks there are, of course, open spaces, through which the
air obtains access to the flame, and the current of air is made more rapid
by the use of a very tall chimney. The large amount of heat produced by
the combustion of so much oil in a small space is partly carried off by the
excess of oil which is made to overflow the burner—about four times the
quantity consumed being constantly pumped up into the burner for this
purpose. Lighthouse lamps are made with two, three, and four wicks; and
the oil is forced up in the burners either by clockwork or by the pressure
of a piston loaded with a weight. The following table gives the sizes of the
burners and the illuminating powers of the lamps:
Order of Light.
Number of Wicks.
Diameter in inches.
Intensity of Light in Carcel Lamps.
1
4
3½
23
2
3
215⁄16
15
3
2
1¾
5
The quantity of oil consumed in these lamps is less than that proportional
to the increase of the light:—for example, although the four-wick
lamp gives twenty-three times the light of the simple Argand, it only consumes
nineteen times the quantity of oil. The oil used in these lamps is
colza; but experiments have been made with a view of introducing petroleum,
598which has the advantages, not only of being cheaper and uncongealable
by cold, but of giving a whiter and more brilliant light. Hitherto,
however, this substance has answered only with lamps of one wick.
Coal-gas has been applied to the illumination of lighthouses, and as it
gives a light of great brilliancy and steadiness, when consumed in proper
burners, it has certain advantages over oil lamps, which have caused it to
be employed in situations where a supply can be readily obtained. The
light produced by lime, ignited by the combustion of coal-gas or hydrogen
mixed with oxygen, has also been suggested; but this plan is not without
risk of interruptions and of dangerous accidents, and it has been considered
inadvisable to entrust the apparatus to the persons who commonly take
charge of lighthouses.
The electric light has been very successfully applied in certain lighthouses,
since the mode of producing steady currents by magneto-electric[10]
machines has come into use. The lighthouses at the South Foreland have
been thus illuminated by a machine constructed by Mr. Holmes in 1862.
A very powerful electric light is exhibited from the lighthouse on Cape
Grisnez; and the adoption of this source of light has been extending, as it
is far more intense than any other artificial light, and can be sent in more
concentrated beams across the sea, on account of its being emitted from a
space which is practically a point. These circumstances cause the beams
of the electric light to possess greater power of penetrating the atmosphere
than those from any other source.
10. Now superseded by the dynamo-electric machines.
But it is perhaps in the optical apparatus of lighthouses that the greatest
improvements and most admirable inventions are to be found. When only
the blaze of an open fire furnished the guide to the mariner, the means
resorted to in order to throw across the sea the light which issued from the
flames upwards or landwards, appear to have been of the rudest kind, even
where such attempts were made at all. The inverted cone on the Tour de
Cordouan has been already mentioned, and we read of cases in which
screens of sheet brass were placed on the landward side, to throw back the
light seaward.
Here it may be proper to examine the conditions which determine how
the light can be made most available for the guidance of the mariner.
Everybody knows that the light from a luminous body spreads out from it
in all directions equally. Thus, if we simply place an electric light on a
tower such as that on the Bell Rock, but few of the luminous rays can
benefit the mariner: namely, those which fall upon the sea or are directed
to the horizon. A much larger portion of the light will stream upwards and
be lost in space; another part will descend towards the base of the tower,
and be equally wasted. Again, if the situation of our lighthouse were on
the shore of the mainland, all the light which passes landwards, whether
horizontally or not, would be entirely lost for our purpose. Even if, in the
case of an isolated lighthouse, we can send out all the light in a nearly level
zone over the sea to the horizon, the intensity of the illumination will diminish,
on account of the widening space, as the distance increases. The
question, therefore, arises whether it is possible to send the whole of the
light in one unbroken beam, not liable to this kind of enfeeblement, so that
the only loss it can experience may be absorption by the imperfectly transparent
atmosphere.
There are two means of gathering up all the otherwise useless beams,
and sending them in such a direction as to reach the eye of the distant
mariner. The one is by reflection from mirrors, and the other by refraction
599through lenses. The apparatus employed in the first process is termed
catoptric, and in the latter dioptric.
When a luminous point is placed at the focus of a parabolic mirror, all
the rays which fall upon the mirror are reflected by it in a direction parallel
to its axis, so that they form a cylindrical beam. This is the method which
was adopted in the first improvements effected in lighthouses. The parabolic
reflector was first used at the Tour de Cordouan in 1780, and soon
afterwards metallic reflectors became the ordinary appliances of lighthouses,
and they are still largely used. Such reflectors are made of sheet
copper, thickly plated with silver, about 6 oz. of this metal being applied
to 16 oz. of copper. They are formed by carefully beating a circular sheet
of the plated copper into a concave shape, which is finally brought to the
exact curve by the aid of gauges, and is then turned and polished. The
largest of these reflectors have a diameter of 2 ft. at the mouth, as it is
termed, for the reflector comes forward in advance of the lamp, the chimney
and burner passing through openings in the metal. The flame of the lamp
occupies such a position that its brightest part is in the focus of the mirror;
but since the focus is a point merely, whereas the flame has a certain magnitude,
it follows that the want of coincidence of the other luminous points
with the focus produces a certain divergence in the reflected rays, so that
the beam is not accurately cylindrical. This, however, is far from being a
disadvantage practically, for it has the effect of widening a little the strip
of sea illuminated by the beams. But all that portion of the light which
escapes from the mouth of the mirror without being reflected is radiated
in the ordinary manner, and is practically lost. We shall presently see
how even this light may be gathered up and brought into the main beam.
Let us suppose a number of such reflectors, each with its own lamp,
placed in a horizontal circle, so as to throw their beams towards different
points of the compass. If eight lamps were so placed, eight beams of light
would stream out across the water, like eight spokes of a wheel; eight sectors
would, however, be left unilluminated, and for ships in these spaces the
lighthouse would be virtually non-existent: its rays could only reach vessels
within the eight narrow strips traversed by the beams. If we double the
number of reflectors in the circle, or if we arrange another series of eight
in a circle above or below the others, so that a lamp in the second circle
coincides vertically with an interval in the first, the effect will be that we
shall have sixteen beams, and sixteen dark sectors, instead of eight; that
is, only a very small part of the expanse of water will receive the benefit
of the light. It must be remembered that the breadth of the cylindrical
beam would not be greater than the diameter of the mirrors, and that the
space illuminated by it has the same breadth at all distances; or rather,
that this is nearly the case, for the light does not all issue precisely from
the focus of the mirror. Thus, even if we use a very great number of
mirrors, we shall succeed in illuminating but an extremely small proportion
of the sea horizon. This evil is met by giving a horizontal rotatory
motion to the reflectors, causing the beams to sweep over the whole expanse
of the waters; and thus from every ship the light will be visible for an
instant. The rotation is produced by clockwork, duly regulated, so that
an uniform motion is obtained. The regular appearances and eclipses of
the light prevent the mariner from mistaking for a lighthouse a bright star
near the horizon or an accidental fire on the coast; and, further, it being
necessary that the lighthouses along any particular coast should be readily
distinguishable from each other, it becomes easy, by assigning to each lighthouse
600a different period of revolution, to individualize them, so that the
mariner shall be in no danger of confounding one with another.
But when the lighthouses on a certain extent of coast are numerous, this
mode of distinguishing them becomes inconvenient, as mistakes might
easily be made in small differences of time; and it would be inexpedient
to keep long intervals of darkness. Hence other methods have been resorted
to in addition—such as red lights, or lights alternately red and white.
The following are the distinctions made use of among the Scottish lighthouses,
including the double lighthouses, which give a leading line to the
navigator:
1. Fixed lights.
2. Revolving lights.
3. Revolving, with red and white beams alternately.
4. Revolving, with alternately two white beams and one red.
5. Revolving, with alternately two red beams and one white.
6. Flashing, in which the light increases and decreases at regular intervals.
7. Intermittent, in which, by means of a revolving screen, the light is abruptly cut
off and exhibited.
8. Double fixed lights.
9. Double revolving lights, which appear and disappear at the same instant.
The efficiency of reflectors depends on the state of polish of the surface,
and even with the most brilliant polish there is a very large loss of light:
in the ordinary condition of lighthouse reflectors, it is found that one-half
of the light is lost at the surface of the mirrors. An attempt was made in
England, about the beginning of the present century, to substitute glass
lenses for mirrors. But it was found that, in spite of the loss occurring
in reflection, the mirrors produced a more intense beam. No doubt the
person who made the attempt did not observe the true conditions of the
problem. It was Fresnel, the illustrious Frenchman, whose name has
already been mentioned in these pages, who successfully solved the problem.
He saw that it would be necessary to give the lenses a short focal
length, and at the same time to have their diameters very great. The
dimensions required by these conditions far exceeded any that could be
given to lenses formed in the ordinary manner; and even if they could be
so formed, the great thickness of glass which would be necessary would
diminish the transparency, and unduly increase the weight of the apparatus
to the detriment of the revolving apparatus. An idea now occurred to
Fresnel’s mind, which, although similar to previous projects, he conceived
independently, and was undoubtedly the first to carry out. This was the
idea of the lentille à échelons, or “lens in steps.” The construction of this
will be understood from Fig. 305, where a b is a section of a lens in steps,
and the dotted line, c, shows the thickness an ordinary lens of the diameter
a b would have. Fresnel kept only the marginal part of such a lens; and
inside of the ring formed by this, he fitted the margin of a second large
lens having the same focal distance; inside of this another ring, and so
on; and in the centre a large lens of moderate thickness. He also placed
above and below the lens the concentric prisms, e e´ and f f´, which, by refraction
and total reflections (see page 399), send the rays parallel to the axis
of the lens. Fresnel also contrived methods of economically grinding such
lenses and prisms with precision.
Fig. 305.—Revolving Light Apparatus.
Fresnel saw that it would be useless to apply lenses in lighthouse illumination
unless the intensity of the light given out by the single-wick Argand
lamps then in use could be considerably increased, without much enlarging
601the flame. Accordingly he devoted himself, in conjunction with his friend
Arago, to this preliminary consideration. Their studies and experiments
led them to the construction of the lamp with several concentric wicks—by
which a brilliancy of light is obtainable twenty-five times greater than that
of the single-wick Argand. The light which the improved lamp, when combined
602with Fresnel’s lenses, could send to the horizon, was equivalent to
that which would be given by the united beams of 4,000 Argand lamps
without optical apparatus; and it was eight times greater than any which
could be produced by the reflectors then in use. The first apparatus constructed
on Fresnel’s plan was placed on the Tour de Cordouan in July, 1823.
France led the van in the erection of the most perfect lighthouses in the
world, and it was not until 1835 that, by the strenuous advocacy of Mr.
Alan Stevenson, a dioptric apparatus was employed in a British lighthouse;
but at the present time Fresnel’s principle has been adopted in the majority
of British lighthouses. Fig. 305 is a part elevation, with the section, of a
catadioptric apparatus of the first class. In plan it is a regular octagon,
and it sends out eight beams, which are directed to the horizon, and made
to sweep over the sea by its regular rotation, produced by clockwork contained
in the case, A. The whole frame is very accurately balanced, and
turns on its bearings, and the rollers, h, h, with great smoothness and
steadiness. The moving power is given by the descent of a weight attached
to a chain or cord, which is wound round a barrel. One train of wheels is
connected with apparatus for regulating the speed, and to this an indicator
is attached which registers the number of revolutions made in an hour.
There is also a contrivance of some kind for maintaining the motion while
the weight is being wound up. The reader will observe that all the light
of the lamp, L, is utilized, except that which is directed towards the base
and top of the apparatus—a quantity less than one-fifth of the whole.
About 45 per cent. of the light emitted by the lamp falls on the refracting
lenses; 22½ on the upper reflecting prisms; and 13½ on the lower reflecting
prisms. The brightest part of the flame is placed so that the beams
from it are directed towards the sea horizon, and the space between the
horizon and the neighbourhood of the lighthouse receives ample light from
the other parts of the flame. Thus a ship, or any part of the sea within
the range of the lighthouse, will see the light appearing at regular intervals,
as one after another of the eight beams passes across it, the intervals being
one eighth of the time in which the apparatus completes its revolution.
The zones of totally reflecting prisms, shown at e e´, f f´, Fig. 305, were not
adopted in British lighthouses until 1844, when the Skerryvore light was
exhibited with the complete apparatus represented in the drawing.
The optical apparatus for lighthouses is constructed of certain sizes,
adapted to the different situations in which it is to be used. The apparatus
we have just described is made in six forms, according to the order
of light required. The first three orders are for sea lights, the rest for
harbour lights; and the following are the dimensions of the apparatus for
each order of revolving or fixed lights:
Order.
Height in Inches.
Internal Diameter in Inches.
Number of Reflecting Prisms.
In Upper Zone.
In Lower Zone.
1
106½
72½
18
8
2
83½
55
16
4
3
61½
39½
11
4
4
29
19¾
5
4
5
21¾
14¾
5
4
6
17½
12
5
4
603When a revolving apparatus of the above description is erected on shore,
a reflector of suitable shape and dimensions is placed on the landward side
of the lamp, so as to throw its rays back upon itself and towards the lenses
which are directed seaward.
Fresnel also constructed glass apparatus for fixed lights. If we require
to send the light equally towards the horizon in all directions at once, the
problem is capable of solution, either by a proper form of glass apparatus
or by a proper form of mirrors. Suppose the section, e c f, Fig. 305, to
revolve about a vertical axis passing through the lamp, it would sweep out
a form which, when executed in glass, would spread out all the light falling
upon it into one horizontal sheet. Fresnel was obliged to content himself
with an approximation to this shape, formed by a prismatic frame of many
sides, containing straight horizontal bars of glass, having the section e c f.
The light is not quite uniformly distributed by such apparatus, but the difficulty
and expense attending the formation of prismatic rings were very
great when Fresnel constructed this apparatus. Such rings can now be
produced economically and accurately, and therefore the fixed-light apparatus
is now constructed of circular glass rings, mounted in sections in such
a manner that a vertical section through the axis of the apparatus would
cut them in the form represented at e c f. Instead of forming the metal
framework in which the glass is mounted with vertical ribs, it is made with
the ribs placed somewhat diagonally, in order that the dark sectors which
would be produced by the shadows of upright ribs may be avoided. It
should be understood that the forms of the glass in each side of the octagonal
apparatus represented in the figure are produced by the revolution
of the same section, e c f, about the horizontal axis, d g.
An ingenious promoter of the catoptric system has contrived to solve the
same problem by mirrors. The form of these may be understood by the
aid of Fig. 306, which, however, relates to another contrivance. Suppose
that the lines A B, A´ B´, are turned about C D as an axis, all three preserving
their relative positions, A B and A´ B´ would sweep out two parabolic cones,
which would have the property of reflecting in a horizontal direction all
rays falling upon them from a lamp placed at L. But glass, as a material
for lighthouse apparatus, has so many advantages over metal that it is probable
that metallic reflectors will soon be entirely obsolete. The polish of
the metal is very readily destroyed, and as it is constantly liable to be tarnished,
the frequent cleaning required is apt to produce a scratched state of
the surface, even when great care is used. Far greater accuracy of form can
be imparted to glass than to metal reflectors. And then there is the great
loss of light occurring at even the most highly polished surfaces of metal:
a loss which is far greater than that occasioned by the refraction and reflections
of the glass apparatus. There are cases, however, in which it is desirable
to throw the whole of the light into one beam, and this cannot be done
without reflecting the light from one side. Mr. Alan Stevenson contrived
an excellent apparatus for this purpose, and the diagram, Fig. 306, will
explain its nature. L is a point representing the source of light, A B, B´ A´, a
parabolic metallic mirror. All the rays between L A and L B, and all between
L A´ and L B´—that is, all those which fall upon the mirror—will be
reflected parallel to L G; but those between L B and L B´ would escape from
the mouth of the mirror, B B´, as a diverging cone. This is prevented by
placing the lens, H I, the focus of which is at L, so as to convert the diverging
cone, I L H, into the cylindrical beam, E H I F; and thus half the light
emitted from the luminous point is sent in one direction. A hemispherical
604reflector, C K D, of which L is the centre, receives the other half, which is
thus thrown back through L, and then follows the same course as the direct
rays. For the metallic reflector, C K D, Mr. Stevenson afterwards substituted
a system of glass zones; of which O P Q represents the sections.
These had the same effect as the metallic reflectors, without the loss of
light occasioned by the latter. The inner surface of the glass, C K D, is hemispherical,
and the prismatic zones are such as would be produced by turning
the section about L K (or C D) as an axis. The dotted lines show the course
of a ray of light, Lm, which, meeting the hemispherical surface perpendicularly,
passes straight through it, and is totally reflected at m by the inclined
surface, and again at n, so that it returns to L by the path nL. Reflecting
glass prisms were also substituted for the metallic mirror, A B, B´ A´, and thus
the use of metal has been entirely dispensed with in this apparatus. This
light has been termed by Mr. Stevenson the holophotal (ὁλο, entire, φως,
light). Such an apparatus will form the intensest beam that a given source
of illumination can yield. On the other hand, when a fixed light is distributed
to the whole horizon simultaneously, the illuminating power of the
source is taxed to the utmost. These two cases may be considered the
extreme modes of disposing of the light, while the parcelling of it into several
beams, as effected by the apparatus represented in Fig. 305, is an intermediate
mode.
Fig. 306.—Stevenson’s Holophotal Light.
It may be interesting to mention that the holophotal light at Baccalieu,
in Newfoundland, is visible in clear weather from another point 40 miles
distant. So long a range as this is seldom possible at sea, on account of
the rounded form of the earth rendering it necessary to raise the light
nearly 1,000 ft. above the water, if it is required to be visible at 40 miles’
distance. A shorter distance generally suffices for the requirements of the
navigator; and therefore lighthouse towers rising from the water are seldom
carried to a greater height than something between 100 ft. and 150 ft.
A light elevated 100 ft. above the water would be seen from the deck of a
vessel 14 miles distant, and from the masthead a much greater distance.
The optical apparatus of a lighthouse is protected by an outer metal
framework glazed with thick plate glass. This framework is made of iron,
605or of gun-metal—the latter being preferred on account of the frequent painting
which iron needs in order to preserve it from corrosion. The glass is
carefully fitted into the framework, so as to avoid exposure to strains from
the shocks and vibrations to which a lighthouse is exposed. The keepers
are always provided with a store of panes of glass, ready for fitting into
their places in case of accidents. Sometimes the glass is broken by large
sea-birds dashing against it, and by pebbles which are thrown up by the
waves, or driven by the wind against the panes. It is the interior of this lantern
which forms the light-room already spoken of. Great pains have been
bestowed on the proper ventilation of these light-rooms, as not only must
the air have access to the lamp to supply the flame, but the carbonic acid
which escapes from the chimney of the lamp must be promptly removed.
Another serious inconvenience of an ill-ventilated light-room would be the
condensation, in the inner surface of the plate glass, of the aqueous vapour,
which is also a product of the combustion.
The lenses and circular prisms for lighthouses are usually made of crown
glass, and are ground by fixing them on a large revolving iron table, on
which they are bedded in plaster of Paris and cemented by pitch—great
care being taken to place them in the exact position required, for only
about one-eighth of an inch is allowed for grinding down to shape the glass
as it comes from the moulds. Sand, emery, and finally rouge, are used
with water for the grinding and polishing processes. The cost of the optical
apparatus alone of a light of the first order, like that shown in Fig. 305,
amounts to upwards of £1,500. The lenses and prisms are very carefully
adjusted in their framework after this has been fixed, and no plan of testing
the adjustment has been found more efficient than that of viewing the sea
horizon through them from the position which the flame will occupy.
The men to whom the charge of a lighthouse is confided undertake a
duty involving the gravest responsibilities, and demanding unremitting care.
In those lighthouses where a number of reflectors are hung upon a revolving
frame, the extinction of one lamp may not be a matter of much consequence;
but where only one lamp is used, life and death depend upon its
burning. To isolated lighthouses—such as those of Skerryvore and the
Bell Rock—four keepers are appointed, and one of these is always on shore
on leave, so that the men may be relieved at intervals; for it has been
found that a residence in these lonely towers cannot be continued long together
without bad effects. The duties of the lighthouse-keepers must be
performed with the greatest regularity. The glasses of the light-room and
the optical apparatus are carefully cleaned every morning; the lamps are
supplied with oil, the wicks trimmed or renewed, the machinery oiled and
adjusted, and everything prepared in readiness for the evening. At sunset
the lamps are lighted, and one keeper takes his watch until midnight, when
he is relieved by another, who maintains the vigil till sunrise, when the
lamps are extinguished.
The expediency of the regulation appointing three men to be always
at the lighthouse may be illustrated by an incident which occurred about
the beginning of the present century at the lighthouse on the “Smalls,” a
rock in the Bristol Channel. Two keepers held watch over the light on
that rock, which for months together is sometimes cut off from all communication
with the shore. At the time alluded to, after the weather had
for two weeks prevented access to the lighthouse, it was rumoured among
the seafaring men of the neighbouring ports that something was wrong at
the “Smalls,” for a signal of distress had been observed; but the boats
606could not go within speaking distance, although many attempts were made
to reach the rock. The relatives of the men became anxious, and night
after night watched for the light. But the light never failed to appear at
the proper hour. After four months came calmer weather, and then a boat
brought to shore one lightkeeper alive, the other dead. What the former
felt when he found his comrade to be dying in their dreadful isolation, or
what his emotions were when he found himself there alone with the lifeless
body, is not recorded. But the thought occurred to him that he must not
commit the body to the waves, lest any suspicion of foul play might fall
upon himself. He therefore contrived a sort of coffin for the dead man,
and dragging it up to the gallery of the lighthouse, tied it there. Punctually
and faithfully for four long months did he perform all the duties of his
position, keeping watch from twilight till dawn in that lonely light-room,
while his ghastly charge remained there within sight. But he came on
shore strangely altered—a sad, silent, gloomy, worn man—so that even his
intimate friends hardly knew him.
Here we close this brief account of the modern lighthouse, and of its
beautiful appliances, by which Science “has given new securities to the
mariner,” in addition to those with which she furnished him when she
showed him the use of the compass, supplied him with the chronometer,
and placed the sextant in his hands. How anxiously must the seaman
who has been prevented by unfavourable skies from ascertaining his exact
position, and has been trusting to the log and the compass to work his
reckoning, scan the horizon for the first glimpse of the hospitable light
beacon, which seems to say that the country he is approaching has been
watching for his coming, and welcomes him to its shores.
607
Fig. 307.
PHOTOGRAPHY. — PHOTOGRAPHY IN COLOURS.
No other of our nineteenth century inventions is at once so beautiful, so
precious, so popular, so appreciated as photography. It is exercising
a beneficial influence over the social sentiments, the arts, the sciences of
the whole world—an influence not the less real because it is wide-spread
and unobtrusive. The new art cherishes domestic and friendly feelings by
its ever-present transcripts of the familiar faces, keeping fresh the memory
of the distant and the dead; it keeps alive our admiration of the great and
the good by presenting us with the lineaments of the heroes, the saints, the
sages of all lands. It gratifies, by faithful portrayals of scenes of grandeur
and beauty, the eyes of him who has neither wealth nor leisure for travel.
It has improved pictorial art by sending the painter to the truths of nature;
it has reproduced his works with marvellous fidelity; it has set before the
multitude the finest works of the sculptor. It is lending invaluable aid to
almost every science. The astronomer now derives his mathematical data
from the photograph; by its aid the architect superintends the erection of
distant buildings, the engineer watches over the progress of his designs in
remote lands, the medical man amasses records of morbid anatomy, the
geologist studies the anatomy of the earth, the ethnologist obtains faithful
transcripts of the features of every race. To the mind of an intelligent
reader numberless instances will present themselves, not only of the utility
of photography in the narrower sense of the term, but of its higher utility
in ministering to our love of the beautiful in art and in nature.
Effects produced by chemical changes to which the rays of the sun
give rise are matters of common observation. The fading of the colour
608in the portions of a fabric which are exposed to the light is a familiar instance;
and the bleaching of linen under the influence of sunshine in the
presence of moisture is a well-known operation. Decompositions produced
by light in certain compounds of silver soon attracted the attention of
chemists, and the remarkable activity of the solar rays in causing the combination
of hydrogen and chlorine gases has been even made the means
of measuring the intensity of light. When equal volumes of these two
gases are mixed together in the dark, they may be kept for an indefinite
period without change, provided only that the mixture be preserved from
access of light. But the instant it is exposed to the direct rays of the sun,
or to an intense light, such as that of burning magnesium, the two gases
suddenly unite with a loud explosion, in which the glass vessel containing
them is shattered into atoms. The product is an intensely acid invisible
gas, called hydrochloric acid; and if the mixture is exposed to the diffused
light of day, instead of the direct rays of the sun, then the production of
hydrochloric acid will take place gradually, and with a rapidity depending
on the intensity of the light.
Of vastly more importance than the small operations of the laboratory
and the bleach-field are the changes which the sun’s rays silently and unobtrusively
effect in the vegetable world. The chemical effect of light here
appears to reside in its power of separating oxygen from substances with
which it is combined. The green parts of plants absorb from the atmosphere
the carbonic acid gas, which is constantly produced by the respiration
of men and animals, and by combustion, and other processes. Under
the influence of sunshine, this carbonic acid is decomposed within the
tissues of the plant; the oxygen is restored to the atmosphere; the carbon
with which it was united is retained to build up the structure of the plant.
In a similar manner light separates the oxygen from the hydrogen of water,
and the former gas is given off by the leaves, while the hydrogen enters
into the composition of the plant. The carbon, which forms so large an
element in the food of plants, is chiefly obtained in this way; and the
abundance of the supply of oxygen thus thrown into the atmosphere may be
inferred from the fact that a single leaf of the water-lily will in the course
of one summer give off nearly eleven cubic feet of oxygen. But for this
continual restoration of oxygen to the atmosphere, animal life would soon
disappear from the face of the earth. It is the office of the vegetable world
not only to furnish a supply of organic matter as food for animals, but when
the materials of that food have been converted into oxidized products in
the animal system, and returned to the atmosphere as carbonic acid and
aqueous vapour, the sunshine, acting on the vegetable structure (chiefly on
the delicate tissue of the leaf), tears apart the oxygen and the other substance.
These are, therefore, once more capable of combination, by which
they may again supply the animal with heat and the other energies of life.
Those actions of light which have been last referred to are called by the
chemist reducing actions, a term which he applies to the cases in which a
compound is made to part with its oxygen or other similar element: when
the remaining ingredient is a metal, the operation by which the other has
been removed is always called reduction. On the other hand, the inverse
operations by which oxygen, chlorine, &c., are fixed upon other bodies, are
distinguished as processes of oxidation. Light is the means of determining
each of these kinds of changes, according to the conditions and the nature
of the substances exposed to its action. Thus moist chloride of silver will
retain its white colour if preserved in the dark; but if exposed to sunlight,
609it quickly acquires a violet tint, which deepens in intensity until it has become
black. The dark matter was formerly admitted to be silver; for it
was known that the finely divided metal has this appearance, that during
the process the compound gives off chlorine, and that when nitric acid is
poured upon the darkened matter, reddish fumes are given off, exactly as
when the acid acts upon pure silver. The use of silver nitrate as a marking-ink
for linen depends upon a similar alteration of the salt within the
fibres; and the same reduction takes place when to a solution of the nitrate
in water organic matter is added. If a piece of white silk be dipped into a
solution of chloride of gold, and exposed to the sun’s rays while still wet,
the silk becomes first green, then purple, and finally a film of metallic gold
will be found overspreading its surface. Many other chlorides and analogous
compounds are similarly affected by sunlight. On the other hand,
chlorides, as we have already seen, and oxygen, fix on hydrogen and on
organic substances with greater energy under the influence of light. A
large series of chemical compounds are obtained by means of the augmented
affinity of chlorine for hydrogen induced by the rays of the sun.
It was in availing himself of an action of the latter class that, in 1813,
Joseph Nicéphore Niepce[11] established photography; for he was the first to
obtain a permanent sun-picture. Twelve years before this, Wedgwood and
Davy had copied paintings made on glass, and the profiles of objects, the
shadows of which were projected upon a piece of white paper, or white
leather, saturated with a solution of nitrate of silver. The images so obtained
could not be fixed, as no means was then known of removing the
silver salts which had not been acted upon during the exposure; and the
pictures soon blackened in every part when exposed to the light. The
application of the camera obscura, and the fixing of the image so obtained,
define the commencement of the art of photography. The process of
Niepce, which was termed heliography, was conducted by smearing a highly
polished metallic plate with a certain resinous substance known as “bitumen
of Judæa,” and this was exposed to the image formed in the camera
for some hours. The action of the light was such, that the resin, which
before exposure was soluble in oil of lavender, became insoluble in that
substance. Hence, on treating the plate after exposure with that solvent,
only the deep shadows dissolved away, the lights being represented by
the undissolved resin. The brightly polished parts of the plate, which
were uncovered by the removal of the resin, appeared dark when made
to reflect dark objects, while the resin remaining unchanged on the plate
appeared light in comparison.
In 1826 a French artist, named Daguerre,[12] who had already made some
reputation as a painter of dioramas, entered into a sort of partnership with
Niepce, into whose process he introduced some improvements; but, dissatisfied
with the slowness of this proceeding, he invented a process of his
own, by which pictures of great beauty could be produced with all the
shadows, lights, and half-tints faithfully rendered; while the time of
exposure in the camera was reduced to twenty minutes. In this process
the burnished surface of silver formed the shadows. A plate of copper,
coated with pure silver, had the silvered surface polished to the highest
degree, and it was then exposed to the vapour of iodine until a thin yellow
film had been produced uniformly over the silver. It was then placed in
610the camera; and, although when withdrawn no image was perceptible, a
latent image was nevertheless present; for when the plate was exposed to
the vapour of mercury, that substance attached itself to the parts of the
plate in proportion as they had been acted upon by the light. Means
were adopted by Daguerre for fixing the picture; and after his processes
had been made public in 1839, several important improvements were
proposed by other persons. By using bromine as well as iodine the sensitiveness
of the plates was so much increased that the time required for
exposure was reduced to two minutes, so that about the year 1841 portraits
began to be taken by this process.
The world at large, which profits most by great inventions, has little idea
at what cost of intense application, concentrated thought, and heroic perseverance,
such discoveries are made. What his discovery must have cost
Daguerre may be inferred from an anecdote related by J. Baptiste Dumas,
the distinguished French chemist and statesman. At the close of one of
his popular lectures in 1825–-fourteen years before Daguerre had perfected
his process—a lady came up to him and said, “Monsieur Dumas, I have
to ask you a question of vital importance to myself. I am the wife of
Daguerre, the painter. He has for some time let the idea possess his mind
that he can fix the images of the camera. Do you, as a man of science,
think it can ever be done, or is my husband mad?” “In the present state
of our knowledge we are unable to do it,” replied Dumas; “but I cannot
say it will always remain impossible, or set down as mad the man who
seeks to do it.” The French Government, with an honourable recognition
of the merits of Daguerre, and of Niepce who had passed away poor and
almost unknown, awarded to the former a pension of 6,000 francs (£240),
and to Isidore Niepce, the son of the latter, a pension of 4,000 francs,
one-half to be continued to their widows.
But Daguerre’s process had no sooner been brought to perfection than
it began to be supplanted by a rival method, devised by an Englishman,
Mr. Fox Talbot, who had published his process six months before that of
Daguerre was given to the world, and who, therefore, was unacquainted
with the details of the latter. The first of Mr. Talbot’s publications contained
only an improved mode of preparing a sensitive paper for copying
prints, by applying them to it and causing the light to pass through the
paper of the print, so that the parts of the sensitive paper protected by the
opaque black lines were not acted upon by the light. The paper was first
dipped in a solution of chloride of sodium, and then in one of nitrate of
silver, the result being the formation in the pores of the paper of chloride
of silver, a substance much more quickly affected by light than the nitrate
of silver used by Davy and Wedgwood. The impression so obtained was
a negative, that is, the lights and shades of the original were reversed;
but when this negative was again copied by the same process, it produced
a perfect copy of the original print, for the lights and shades were of course
reversed from those in the negative proof. Thus from one negative any
number of positive or natural copies could be produced; and this point
in Mr. Talbot’s invention is one great feature of photography as now
practised. In 1841, Mr. Talbot obtained a patent for a process he called
the Calotype, but which, in his honour, has since been known as the Talbotype.
A sheet of paper is soaked, first in a solution of nitrate of silver,
and then in one of iodide of potassium, by which it becomes covered with
iodide of silver; it may then be dried. It is prepared for the camera by
brushing it over with a solution of gallic acid containing a little nitrate of
611silver. By this last process its sensitiveness is greatly increased, and an
exposure in the camera for a few seconds, or minutes, according to the
power of the light, suffices to impress the paper with a latent or invisible
image, which reveals itself when the paper is treated with a fresh portion
of the gallic acid mixture. The Talbotype is the foundation of the methods
of photography now in general use; but, before we describe these, it may
be proper to mention some other substances which have been found sensitive
to light, and to discuss the nature of the invisible images which are
first produced in these processes.
The art of photography has outstripped the science—in other words, the
nature and laws of the chemical actions by which its beautiful effects are
produced are not yet clearly understood, and some quite recent discoveries
seem to show that we have yet much to learn before a complete theory of
the chemical action of light can be proposed. Some results which have
been established may be mentioned, as they show those curious effects of
light to be more general than would be supposed from a description of
photographic processes dependent on silver salts only. It has been found
that certain acids, certain salts, and certain compounds containing only
two elements—of which one is a metal—have a tendency to split up, or
resolve themselves into their several constituents, when exposed to the
action of light. On the other hand, chlorine, bromine, and iodine exhibit,
under the same conditions, an exalted affinity for the hydrogen of organic
matters. These tendencies concur when the compounds above referred
to are associated with organic materials, as in photography. Solution of
nitrate of silver is blackened when it is exposed to light on a piece of paper
which has been dipped into the solution; but a piece of white unglazed
porcelain similarly treated shows no change. A solution of nitrate of
uranium in pure water is not changed by light; but a solution of the same
salt in alcohol becomes green, and deposits oxide of uranium. The reducing
action of the light is insufficient of itself to accomplish the decomposition
of the salt in the first case; but the presence of the organic matter
determines this decomposition in the second case. Bichromate of potassium
is by itself not easily decomposed by light; but when it is mixed with
sugar, starch, gum, or gelatine, the sunbeams readily reduce it. It is remarkable
that the gelatine, gum, or starch becomes insoluble by thus taking
up oxygen, and the gelatine loses its property of swelling up in water. We
shall presently see the advantages which have been drawn from these
circumstances.
It is not necessary that the light should act upon both the organic substance
and the oxidizing substance at the same time. If paper impregnated
with iodide of silver and gallic acid be placed in the camera, the image
soon appears; but if, as in the Talbotype, the iodide of silver only be acted
upon by the light, no image is perceptible on withdrawing the paper from
the camera. The action of the light has nevertheless imparted to the silver
salt a tendency to reduction; for when the paper is afterwards dipped into
a solution of gallic acid, the image immediately appears. In order to distinguish
these two actions, the substance which receives and preserves the
latent impression from the light is called the sensitive substance, and that
which reveals the latent image is termed the developing substance. A
considerable number of substances having this relation to each other have
been observed, and the following table of instances—cited by Niepce de
Saint-Victor, the nephew of the original inventor—will give some idea of
their variety:
612
Sensitive Substances in the paper exposed to the action of the Light.
Developing Substance.
Results.
None, i.e., plain paper.
A salt of silver
Black image.
Nitrate of silver, or iodide of silver.
Gallic acid, or sulphate of iron.
Black image.
{ Water
By prolonged action of light, a grey image of protoxide of uranium; the image disappears when paper is kept in the dark, but shows itself again in the light.
Nitrate of uranium.
{
{ Red prussiate of potash
Intensely red positive image; becomes blue by sulphate of iron.
Nitrate of uranium and tartaric acid.
Nitrate of silver or chloride of gold.
Unchangeable images—resembling those of ordinary photographs.
Chloride of gold.
Nitrate of uranium, sulphate of iron, sulphate of copper, bichloride of mercury, salt of tin.
. . . . . .
{ Sulphate of iron
Blue-black image.
Gallic acid.
{
{ Red prussiate of potash
Blue image.
Red prussiate of potash.
Water, bichloride of mercury, gallic acid, salt of silver, salt of cobalt.
Blue image, hastened by acids and by heat.
Bichloride of mercury.
Protochloride of tin, soda, potash, sulphide of sodium.
. . . . . .
Chromic acid, or bichromate of potash.
Salts of silver
Purple-red positive image.
{ Blue litmus
Red image.
Starch.
{ Iodide of potassium
Reddish brown image.
{ White indigo
Blue positive image.
{ Campeachy wood
Red positive image.
These are only a few of the instances in which actions of this kind have
been observed. It is remarkable that the order of the first two columns in
this table may be inverted without changing the result. Thus, instead of
exposing iodide of silver to the light and developing the image with gallic
acid, one may expose a paper saturated with gallic acid solution, and
develop with iodide of potassium and nitrate of silver. The first reaction
noted in the table deserves some remark: it is not peculiar to paper, but
is common to most organic materials, such as albumen, collodion starch,
613fabrics, and indeed to organic matters in general, provided they are not of
a black colour. Tartaric acid, sulphate of quinine, and nitrate of uranium
increase this sensibility. The paper which has been impressed preserves
its undeveloped image for a prolonged period if kept in darkness; and it
has been found that one piece of paper can impart the image to another
by simple contact in the dark. What is still more remarkable, the invisible
impressions on a piece of paper may be transferred to another not in contact
by merely placing it opposite the first, and separated by an interval
of a quarter of an inch. No satisfactory explanation of these phenomena
has been advanced, but many conjectures have been made. One of these
supposes that some unknown intermediate products are formed, which are,
in the case of the latent image on paper, very oxidizable; but in the case
of silver salts, &c., very reducible, so that the addition of a silver salt in
the first case, and of organic matter in the second, only completes the
phenomena by ordinary chemical action. Niepce de Saint-Victor, however,
found that a surface of freshly broken porcelain alone will receive a
latent impression from light, and will reduce in those places sensitive
salts of silver. He believes that the light in these latent images is simply
stored up, and that its energy remains fixed to the surfaces until the occasion
of its producing a chemical action.
When a pure solar spectrum is made to fall upon paper rendered sensitive
by silver salts, the effect is observed to be greatest near the Fraunhofer
line H (No. 1, Plate XVII.), and it is prolonged with decreasing intensity
beyond the violet end of the spectrum, while towards the other end it
terminates about the line F. When other sensitive substances are used,
the range of photographic power in the spectrum is modified. It has been
found that when a daguerrotype plate which has been impressed by the
light in the camera is afterwards exposed to the red or yellow rays of
the spectrum, it loses its property of condensing the mercurial vapours.
This destruction of photographic impression by red or yellow light has a
practical application of great importance, for it permits the processes of
preparing paper and plates to be carried on in a laboratory lighted by
windows having yellow or red, instead of the ordinary colourless, glass.
Thus we see that it is by no means the whole of the solar rays which are
concerned in producing photographic images; nay, there are some which
even tend to destroy the impressions produced by others. The fact that
it is not the light, but only certain rays in the sunbeam, may be proved
very conclusively by an experiment with a glass bulb filled with a mixture
of equal volumes of hydrogen and chlorine gases. When such a bulb is
exposed to the light of the sun or of burning magnesium, which is made
to reach it by passing through a piece of red glass, no explosion takes
place; but if the bulb be covered only with a piece of blue or violet glass,
the explosion is produced just as quickly as if it were exposed to the unaltered
rays.
The visible spectrum obtained in the experiment described on page 318
is far from constituting the only radiations which reach us from the sun.
For invisible beams of heat, less refrangible than the red rays, are found
beyond the red end of the spectrum; and another invisible spectrum
stretches far beyond the violet end, formed of rays recognized only by
their chemical activity. It is these which effect photographic actions, and
though they are in part more highly refrangible than any of the rays producing
the visible spectrum, a large portion are refracted within its limits,
so that the maximum of photographic action in a spectrum is usually near
614the violet end. When we wish to examine the spectrum of the heat rays,
it is necessary to replace the glass prism by one made of rock salt, for
glass absorbs these heat rays. It also intercepts a great part of the most
refrangible rays; for when a prism of quartz is substituted for the glass
one, the spectrum becomes greatly extended at the violet end. The dark
Fraunhofer lines which cross the visible spectrum are represented also in
great numbers in the invisible spectrum: in photographs of the ultra-violet
rays more than 700 dark lines have been counted. It has been
proposed to employ quartz lenses in the photographic camera; but there
is reason to believe that the increased transparency of such lenses for the
chemical rays would be counterbalanced by certain disadvantages attending
the use of quartz.
The beauty of the images which are formed in the camera obscura long
ago gave rise to the desire of fixing them permanently. We know how
perfectly photography has already satisfied that desire, so far as the forms
are concerned. The very perfection of the results obtained in this direction
increases our regret at our inability to fix also the colours, and secure
the picture, not in grey or brown tones of reduced silver, but with all the
glowing hues of nature. An observation made by Herschel, Davy, and
others, seemed at one time to hold out hopes of a possible realization of
chromatic photographs. It was noticed that the images developed upon
chloride of silver, of the different parts of the solar spectrum, partook
somewhat of the colours of the rays which produced them. Edmond
Becquerel made a plate of polished silver, placed in dilute hydrochloric
acid, form the positive pole of a battery. The plate thus became coated
with an extremely thin layer of chloride of silver, which, as its thickness
augmented, exhibited the series of colours due to the action of light on
thin films. The operation was stopped when the plate had become of a
violet colour for the second time; it was then washed, dried, polished
with the finest tripoli, and heated to 212° F., the whole of these operations
having been carried on in the dark. When this plate was exposed for
about two hours to the solar spectrum, fixed by proper appliances which
counteracted the apparent motion of the sun, the luminous rays were found
to have impressed the plate with their respective colours. The yellow was
somewhat pale, but the red, green, and violet were exhibited in their true
tints. A theoretical explanation has been advanced, which supposes that
yellow light, for example, renders the surface of the plate on which it falls
peculiarly capable of receiving and transmitting vibrations corresponding
to those of yellow light. Just as a stretched cord responds to its own
musical note, the modified plate gives back, out of all the vibrations which
fall upon it in ordinary light, only those of which it has itself acquired the
periodicity. But since the plate has not lost its sensitiveness to take on
other rates of vibrations, it receives other impressions, which first weaken
and then overcome the former, and, therefore, the colour necessarily
vanishes. This kind of difficulty seems to be a necessary concomitant of
every attempt in this direction; and all the hopes founded on results yet
obtained have been disappointed by the rapid fading of the images.
The comparative cheapness and convenience of Talbot’s process, and
especially the facilities which it afforded for the multiplication of proofs,
gave an immense impulse to photographic art. But the irregular and
fibrous structure of paper prevented the attainment of the beautiful sharpness
of outline and clear definition of detail which the plates of Daguerre
presented. Sir John Herschel suggested the use of glass plates coated
615with sensitive photographic films, and Niepce de Saint-Victor succeeded
in fixing upon glass layers of albumen (white of egg) containing the silver
salts, a method which is still used to some extent. The art received, however,
its greatest stimulus from the improvements which ensued on the
application of collodion to this purpose. Collodion (κολλα, glue; in allusion
to its adhesiveness) is the name which has been given to a solution in ether
of gun-cotton, or of a substance nearly allied to it. Its employment was
suggested by Le Grey of Paris, but the late Mr. Archer was the first to
carry the idea into practice, and the process which he described in “The
Chemist,” in 1851, is virtually that which is now almost universally adopted.
This process has now been tested, for nearly a quarter of a century, by the
united experience of photographers all over the world, and it is agreed that
it is surpassed by no other, for it secures every quality which a photograph
can possess.[13] The minor details of the method can be, and are, infinitely
varied; scarcely two experienced photographers will be found working
the process in identically the same manner throughout. Before giving an
outline of the collodion process, it may be well to say something respecting
the chief instrument of photography—the camera.
The ordinary photographic camera is almost too well known to require
description. In its simplest form, Fig. 308, it is merely a rectangular box,
in front of which is placed the lens, which slides in a tube, that its position
may be adjusted so as to bring the rays to a focus on the surface of a
piece of ground glass at the opposite end. This glass is fitted into a light
frame, which slides in grooves, so that it can be raised vertically out of its
position, and replaced by another frame, B, which contains a recess for the
reception for the sensitive plate, and a sliding screen which protects it from
light until the right moment. When this frame is placed in the camera,
the sensitive surface occupies the same position as that of the ground glass,
and the sliding screen is drawn up the moment before the operator removes
from the front of the lens a cap which he places there after adjusting
the focus. The sliding screen is usually made with a narrow strip at
the lower part, joined to the rest by a hinge, so that when it has been drawn
up it may be retained in its position, and placed out of the way, by being
folded down horizontally. There is commonly provision for two plates in
one frame, the slides, &c., being doubled, and the plates placed back to
616back, as shown at B, Fig. 308. The camera is usually made in two parts, as
shown in the figure, that at the back sliding within the other, so that a wider
range for adjustment is obtained, and the same camera may even be used
with lenses of different focal
lengths. Many improvements
have been made in the camera,
by which it has been rendered
more portable, and capable of
more adjustments to suit varying
circumstances. Fig. 309 represents
a “bellows” or folding
camera, which appears to supply
every requirement for the studio.
It is copied from Messrs. Negretti
and Zambra’s catalogue, as
are also the other figures of photographic
apparatus here given.
Fig. 307 represents a camera for
taking stereoscopic views, fitted
with two lenses, so that the two views are taken simultaneously on one
plate.
Fig. 309.
No piece of apparatus used by the photographer is of so much importance
as the lens; for good pictures cannot be obtained without well-defined,
sharp images on the sensitive plate, and these images must have sufficient
intensity to produce the required amount of chemical action in a short
space of time. The formation of an image by means of a lens which is
thickest at the centre is tolerably familiar to everybody; for most persons
must have noticed that the lens of a pair of spectacles, or of an eye-glass,
will produce an inverted image of the window-frame on a sheet of white
paper, held a certain distance behind the lens. But the diagrams by which
the paths of the rays are usually represented seem to convey a false impression
to an ordinary reader, who usually goes away with the idea that
somehow three rays are sent off by the object, and that one goes through
the middle of the lens, and the other two meet it and produce an image.
Let us suppose that, by means of a circular eye-glass, the image of a window
is projected on a piece of white paper: a straight line passing through the
centre of the glass perpendicular to its plane will meet the window and
image each at a certain point. The point in which it meets the image is
the focus of innumerable rays, which issue from the point in the window;
that is, of the whole light sent out in every direction by the point a certain
portion falls upon the lens, and by the refraction it undergoes in passing
through it, the rays are again brought together at the point in the image.
Thus the original point in the object is the apex of a solid cone of rays (if
we may say so), of which the lens is the base, and the point in the image
is the apex of another cone, having also the lens as its base. These cones
would be termed right cones, because their bases are perpendicular to their
axes, or central lines. But they represent the rays from only one point of
the object. Let us now consider how the image of another point is formed,
say one in the highest part of the object which forms an image on the
screen. Those rays which are sent out by this point, and fall upon the
lens, form now an oblique cone, of which the lens is the base, and the central
ray will pass through the middle of the lens and continue its journey
on the other side with little or no change of direction, forming also the axis
617of another oblique cone, constituted of the refracted rays, all of which will
meet together at the lowest part of the image. Similar cones of incident
and refracted rays, all having the lens as base, and all of them cones more
or less oblique, will be formed by the light from each point of the object.
Thus, the rays which issue from each point are brought together again in
a series of points which have the same position with regard to each other,
and collectively form an inverted image.
On carefully looking at the image, say of a window-frame, formed by a
simple lens, the reader will observe two defects. The first is that the image
cannot be made equally clear and well defined at the centre and at the
edges: the adjustment which gives clear definition of one part leaves the
other with blurred outlines. The second defect, which is best seen with
large lenses, consists in coloured fringes surrounding the outlines of the
objects. This depends upon the unequal refrangibility of the various rays,
but it is obviated in achromatic lenses, which are formed of two or more
different kinds of glass, so adapted that the refracting power of the compound
lens is retained, and the most powerful rays of the spectrum are
brought to a common focus. Such are the lenses always used in the
photographic camera, and the skill of the optician is taxed to so combine
them as to obtain, not only the union of the principal rays in one focus,
but the greatest possible flatness of field in the image, the largest amount
of light, the widest angle without distortion of the picture, and other
qualities.
Fig. 310.
Photographers have even been so fastidious in the matter of lenses as to
require all the perfection of finish which is given to the object-glasses of
astronomical telescopes. Mr. Dallmeyer has made photographic lenses
which cost upwards of £250; but it is doubtful whether the pictures formed
by these would show any marked superiority over those produced by lenses
costing only one-fifth of that amount. Fig. 310 shows the construction of
the combination usually employed for taking photographic portraits. A is
a section showing the forms and positions of the different lenses; B is an
external view of the brass mounting of the lens. It is provided with a
flange, C, which is attached by screws to the woodwork of the camera; and
within the short tube, of which this is a part, slides the tube carrying the
lenses, being furnished with a rack and pinion moved by the milled head, E.
D is a cap for covering up the front of the sliding tube. A slit in the tube
admits of plates of metal, perforated with circular openings, being inserted.
618The openings are of various sizes; and these “stops” or diaphragms enable
the operator to regulate the amount of light; and to cut off when required
the rays passing through the marginal parts of the lens.
It now remains to describe in a few words a method of photography
which was, and still is, much practised, namely, the collodion process. The
collodion solution is prepared by dissolving one part of pyroxylin (gun-cotton)
in ninety parts of ether and sixty of alcohol. The pyroxylin for
this purpose may be obtained by steeping cotton-wool for a few minutes in
a mixture of nitre and sulphuric acid, with certain precautions which need
not here be mentioned. To the solution of collodion is added a certain
quantity of iodide of potassium, or of iodide of ammonium; and sometimes
other substances also are mixed with the solution with a view of increasing
the sensitiveness of the plate when ready for exposure. Some of the collodion
solution is poured on a well-cleaned plate of glass, which is placed
horizontally; it spreads over the plate, and the excess having been poured
back into the bottle, the evaporation of the liquids leaves the glass covered
with a thin uniform transparent film, which firmly adheres. The next
operation is to render the plate sensitive by means of the “silver bath.”
This is a neutral solution of nitrate of silver, one part to fifteen of pure water,
which is placed in a trough of glass or porcelain, Fig. 311. By the aid of
a proper support the plate is introduced quickly and steadily into the solution,
immediately after the collodion film has been formed on its surface.
In two or three minutes the layer of collodion becomes impregnated with
iodide of silver, and when taken out of the bath, the plate exhibits a creamy-looking
surface. The operation of sensitizing the plate by the silver bath
must be performed in a room to which no light has access, except that which
has passed through red or yellow glass, or a semi-transparent yellow screen.
The plate is now ready for immediate exposure in the camera. It is
placed in the dark slide, in which it is conveyed to the camera; and there
the image of the object is allowed to fall upon it for a time, which varies,
according to the intensity of the light and the nature of the object, from
3 seconds to 45 seconds. The slide is withdrawn from the camera, and taken
again to the “dark” room, i.e., where only yellow or red light can reach it.
If the plate be now examined, it will be found to present no trace of an image.
A latent one, however, exists; and it is developed by pouring over the
plate a solution of pyrogallic acid—one part to 480 of water, with commonly
a little alcohol and acetic acid added. When it is desired to intensify
the image still more, a few drops of the nitrate of silver solution is
added to the developing solution immediately before pouring it on the
plate. When the picture has become sufficiently distinct, it is washed with
pure water, and then immersed in a strong solution of hyposulphite of soda.
The last operation is termed by photographers “fixing” the picture, and
the substance employed in it is invaluable to the art. It acts as a ready
solvent of all the salts of silver which remain on the plate; and the discovery
of this property of the hyposulphites by Sir J. Herschel, in 1839,
marked an era in photography. The picture is then thoroughly washed in
cold water, in order that the hyposulphite of soda may be entirely dissolved
out. It is then dried, warmed before a fire, and finally the film is covered
with a coat of transparent varnish, by which it is protected from mechanical
injury. The image here is negative—that is, the strongest lights of
the object appear as the darkest tints in the picture, and vice versâ. From
it any number of positive pictures may be obtained by means of the sensitive
paper prepared with chloride of silver as in Fox Talbot’s plan.
619As it is a tedious, and perhaps, in some cases, an impossible operation
to completely remove all traces of silver salts and hyposulphites from
photographs, they have frequently been found to fade; but this is rarely
the case with well-prepared specimens. Processes have, however, been
devised by which absolute permanence is secured for the photograph. One
of the best of these is known as the Carbon Printing Process, and, as
improved by Mr. Swan, it is thus practised:
A solution of gelatine is coloured by the addition of Indian ink, or any
other pigment which will give the desired tone. This solution is spread
over sheets of paper which are then dried. In this condition the paper
may be preserved for any length of time without any special precautions.
When it is required for use, it is floated, with the gelatine-covered side
downwards, in a solution of bichromate of potash, and then dried; but
these operations must be carried on in the dark. The paper is exposed
under a negative photograph, with which its prepared side is in contact.
The effect of the light is to render insoluble the gelatine on all those parts
on which it has fallen, and this action extends to a depth in the layer
proportionate to the intensity of the illumination. The object is, therefore,
to wash away all the soluble gelatine and the colour with which it is mixed;
but this soluble gelatine is mainly on the side of the film which is in contact
with the paper. The gelatine surface is therefore made to adhere to
another piece of paper by means of some substance insoluble in water;
and when this has been done, the whole is immersed in warm water.
Then the soluble gelatine is soon dissolved; the first paper floats off,
and the insoluble gelatine, holding the Indian ink or other colouring matter
in its substance, remains attached by the cement. As the thickness of the
layer rendered insoluble is in proportion to the intensity of the light passing
through each part of the negative, the picture will be presented in all the
proper gradations of light and shade.
Fig. 311.
The “wet collodion” process, that has been described on the preceding
page, maintained an almost undisputed
hold for more than twenty years in the
practice of photography in all branches,
and it was not until after the publication
of the first edition of the present work that
a new era in the art was commenced by
the introduction of what is known as the
dry plate gelatino-bromide process, to which
the present enormous popularity of photography
as a recreative art is due. The
difficulties of manipulation, the necessity
for extensive experience, and for special and
cumbersome appliances were obstacles it
at once removed. And not only so, but
the whole scope of the art was extended;
for work that was before supposed impracticable,
even to the most expert professional
photographer, became the amusement
of the amateur. Here, we may
remark in passing, that photography is
greatly indebted for this, and many other improvements, to the
enthusiasm of the amateur, which has accelerated the development
of the art to a remarkable extent. The collodion process itself admitted
620of being modified as a dry plate method, by coating the film with a
preservative solution of tannin, gum, albumen, or other substance, and
then drying the plates, of course in a dark place. This plan made it possible
to practise out-door photography with ease, and such plates were, at one
time, much used for landscape photography, but they have now been
almost superseded by the gelatine plates. It was Mr. Bennet, who, in
1874, first introduced the use of sensitive emulsions of gelatine, and the
advantages offered by their use, caused them to be soon adopted by landscape
and amateur photographers. In 1878, Mr. Bennet showed, that
these plates could be made wonderfully rapid in their action, so that
portraits, etc., could be taken by them in an unprecedentedly short time.
The preparation of the dry gelatine plates was then commenced on a large
scale, and these were found so convenient, and reliable in use, that they
were adopted by the professional photographers, who had hitherto adhered
to the wet collodion and silver bath, from long habit and established
associations. The collodion processes are, however, still much used, and
are preferred by many to the gelatine plates; indeed, it is admitted, that
only by the former can certain desirable qualities of negatives be obtained,
which are of great importance in some applications of the art.
There are, it need hardly be said, many modifications of the processes
recommended for preparing gelatino-bromide dry plates, and each manufacturer
of the various kinds offered for sale has, no doubt, his own special
plan and formula. In all, a very fine and carefully selected quality of
gelatine is the medium in which the sensitive salts are embedded. An
“emulsion” is prepared by adding to warm gelatine solution exactly
determined quantities of solutions of certain compounds, of which a
bromide (usually bromide of potassium) and silver nitrate are the
essential ones, together with a small proportion of iodide of potassium.
Minute quantities of iodine, hydrochloric acid, etc., are also often prescribed
as additions. The mixture has to be heated, at the boiling
temperature, for three quarters of an hour, then cooled, and mixed with
more gelatine solution, or, instead of using acid and iodine and boiling,
a little ammonia is added. When cold and set, the gelatine is washed
with cold water, while squeezed through canvas, or after it has been cut
into thin strips. It is then drained, dissolved at a gentle heat, and filtered
warm. The clean glass plates are coated over with it, at the temperature
of 120° F., and are set aside in a perfectly horizontal position until the
gelatine has set, when they are placed for twenty-four hours in a drying
cupboard, maintained at 80° F. It will be understood that these
operations are conducted in a room where no light enters, except through
a frame of ruby-coloured glass, and the plates, when dry, are carefully
packed and stored in light-tight boxes. They are marvellously sensitive,
and receive the photographic impression in about one-sixtieth (1 60th) of the
time required for wet collodion plates. Half a second exposure in the
camera may be sufficient to impress the image of a well lighted landscape,
even when a very small stop is used, and it is not unusual to employ
for extra sensitive plates, a so-called “instantaneous shutter,” when the
exposure may be no more than 1 80th to 1 100th of a second, and yet obtain
a perfectly strong image. Dry plates are manufactured in vast numbers
in many large establishments, and the operations are carried on to a great
extent by the aid of machinery, by which the plates are uniformly coated
and automatically carried into drying chambers, etc.
If photography were popular before the introduction of the dry gelatino-bromide
621plates, it has since become a hundred-fold more so. Indeed, the
camera is now seen everywhere, and few are the family circles in which
at least one amateur practitioner of the art is not to be found; indeed,
the technical terms of the art have become “Familiar in their mouths as
household words.” The daguerrotype, notwithstanding its cost, had no
sooner become a practicable process for taking likenesses, than it began
to supersede miniature painting, and how rapidly it rose into general
favour may be inferred from the fact that, in 1850, ten years after its
introduction, it was estimated that in the United States of America, at
least ten thousand persons had made it their profession, and, probably
half as many more were occupied in making and selling chemicals, plates,
cameras, lenses, mounting cases, and other apparatus connected with its
practice. Such being the demand for photographic portraits, at the period
when the sitter had, as we have already seen, to remain motionless for two
whole minutes in sunlight, we can hardly be surprised at the increased
popularity the art has acquired in the last decade, when a picture can be
produced with one-hundredth the length of sitting, and at about the same
reduction of cost. It may here be mentioned, that Daguerre’s process is
still occasionally used for special purposes; it was, for instance, the
method selected for obtaining the photographic records in the expedition
sent out by the French Government, in 1874, to observe the transit of
Venus.
Fig. 311a.—The Roll-Slide.
The dry plate processes have given an immense impulse to landscape
photography, and travellers have been able to bring back authentic representations
of the scenery and inhabitants from every part of the globe.
This advantage arises from the fact that having the camera, and its
appurtenances, the tourist or traveller is not obliged to carry anything
about with him except his plates, and when these have once been exposed
in the camera, and stowed away in light-tight boxes, the latent images
may be developed months, or even years, afterwards. But glass plates
are heavy, and are liable to accidental breakage. Inventive ingenuity
has been actively at work for the past few years, to find a means of obviating
these remaining inconveniences. The first method adopted was to
employ paper instead of glass, as a support for the sensitive gelatine film.
The paper, having been cut to the proper size, is placed on a film-carrier,
which is usually a thin plate of ebonite, by which the paper is kept flat.
These carriers take the place of the glass plates in the ordinary dark slide,
and after exposure in the usual way, the papers are removed in the dark
room and made up into light-tight packages, where, of course, a large
number will occupy but a small space, and the weight of them be wholly
negligible. Many persons make use of this arrangement, which has
the advantages of simplicity and of requiring no special apparatus. But
an improvement was soon brought out, which consists in substituting
for the carriers and pieces of sensitive paper a continuous roll
of the material. For this purpose a special piece of apparatus, called
the roll-holder, is made to take the place of the dark slide at the
back of the camera. The arrangement will be readily understood
from Fig. 311a. The figure shows the apparatus in section, but only
the disposition of the principal parts, most of the mechanical details being
omitted. R R´ are two metallic or wooden rollers, which admit of being
readily put in their places and taken out. Upon one of these, R, the full
length of the material is previously wound, and the free end is passed over
another roller, r´, and across the opening at E O, where the exposure is
622made. There is in front of this a dark slide (not here shown) to be drawn
up when everything is ready for uncovering the lens. Immediately behind
the paper is a flat plate of ebonite, E, or a smooth black board, the object
of which is to keep the material quite flat as it passes over the opening
to the roller, r´, which guides it to the roll, R´, on which it is wound as
required. S S´ are two small rollers always pressed by springs against
the rolls to prevent the turns working loose. There is a registering
apparatus outside in connection with one of the rollers, r, or r´, to show
when the proper length of material has been wound across the opening
for a new exposure; and at the same time a mark is automatically made
on the paper to indicate where the negatives are to be separated for
development by cutting the paper. Some forms of the apparatus also
call the operator’s attention to the sufficient winding of the roll by an
audible signal, a stroke on a little bell tells that everything is ready for a
new exposure. In some cases the number of exposures already made is
registered by figures
that appear on the
outside. The paper
in these processes is
used only as a temporary
support; for
after the negative has
been developed in the
ordinary way, the sensitive
gelatine film is
removed from it and
made to adhere firmly
on a plate of clear
glass, from which
prints are taken as usual. The operations required for the transferring
require considerable dexterity of manipulation, and to both the paper and
the glass special preparations have to be applied, before and after the
transference of the film. This plan, therefore, of “stripping films” involves
so great a number of delicate and somewhat troublesome operations that
very many photographers have preferred to encounter the labour and
risks of carrying about with them the more easily manageable glass
plates. But what if some grainless, transparent substance could replace
the paper in these rolls so that the negatives might be ready for printing
from when merely developed and fixed? Many trials have been made to
find this desideratum. A material sufficiently translucent, even, and of
tenacity enough to bear the stretching strain between the rollers has, it is
believed, been discovered in a very singular substance previously used for
other purposes. The reader is no doubt familiar with it as the substitute
for ivory in combs, knife handles, and other small articles. It is called
celluloid, and is a composition the principal ingredients of which would
never be guessed from its appearance—namely gun-cotton and camphor!
This material is prepared in a plastic condition that enables it to be
shaped into any required form. It can be drawn into threads or rolled
out into very thin films. Thin plates of it have been used in photography
as a substitute for glass, for the sake of lightness, before its employment
as a transparent film in the roll-holders. We have now at length the
equipment of the travelling photographer reduced to the utmost conceivable
limits of lightness and compactness. Thus the complete apparatus
623required for taking hundreds of pictures of a good size need not be more
than a few pounds in weight, and can easily be carried in the hand. But
even quite small negatives can now be very readily printed in a few
seconds on paper, with an enlargement of many times the original
dimensions. The resources of the photographic art appear indeed to be
endless; but a mere statement of even the more interesting of these
would lead us beyond our limits, and descriptions of the details of
manipulation are out of our province altogether. But a few of the more
recent applications and developments of the art scarcely or not at all
alluded to in the foregoing pages should receive some attention.
The extraordinary sensitiveness of the gelatine-bromide film which
makes it possible to impress on it a photographic image in the merest
fraction of a second of time, enables us to take pictures of objects in
rapid motion. Express trains at their highest speed have been successfully
photographed, and so has almost every moving object in nature.
The photographs that have been taken of men, of birds, horses, and other
animals in every phase of their most rapid actions, have solved many
disputed and perplexing problems as to the nature of their movements, and
sometimes the solutions have been of a very unexpected kind. Taking a
photographic “shot” at a bird has become almost more than a figure of
speech; for there are contrivances by which a bird on the wing may be
aimed at with the lens, and hit off on the sensitive plate with a certainty
surpassing that of the fowling-piece. There are also photographic
repeaters by which six or more successive photographs of the bird, etc.,
can be taken in a single second. Mr. Muybridge has published a
number of such photographs of the horse, and by projection of the
different images on a screen from a magic lantern, in rapid succession,
he has been able to reproduce the visual appearance of horses trotting,
leaping, galloping, etc., on the principle of the zoetrope (page 399).
Photography has afforded wonderfully delicate observations in many
departments of science, by recording phenomena too rapid for the eye
to seize, or too recondite for direct perception. A few examples may be
mentioned. First, the advantage of photographing the lines of spectra,
such as those described in our article on the spectroscope, will at once
suggest themselves, and accordingly this method of recording spectra
has been largely used, and in the hands of Mr. Lockyer, Dr. Draper, and
others has been successfully applied to the study of the solar and stellar
spectra. But more than this, it is the sensitive photographic plate that
has enabled us to explore the region of the solar spectrum lying far
beyond its visible limits in the red and in the violet rays. The ultra-violet
portion of the spectrum is shown photographically to be occupied
by multitudes of the thin insensitive spaces—breaks in the continuity of
the active rays—which are impressed on the photographic print as black
lines, similar in every respect to the lines mapped out in the visible
spectrum by Fraunhofer. It is known by these that the ultra-violet
spectrum, produced by glass prisms, extends to a distance beyond the
last visible rays of nearly double the space occupied by the colour
spectrum. The principal lines, or rather the greater groups of lines in
the invisible spectrum, are distinguished by the capital letters of the
alphabet, in continuation of Fraunhofer’s method, beginning from H and
nearly exhausting the letters of the alphabet to designate them. These
are photographed in the dark; for all the solar beams that are allowed to
enter the stereoscope are first passed through blue glass of such a depth
624that every kind of emanation capable of affecting the human eye is
intercepted.
Another extremely interesting example of the application of the art to
scientific research is celestial photography. An image of the sun may be
impressed on a sensitive plate in an ordinary camera, in an amazingly
short space of time, but such image is much too small to show any of
the markings on the disc of our luminary, even when the image is
magnified, for its diameter is only about ⅒th of an inch for each 12
inches of the focal length of the lens. In order to obtain an image of 4
inches diameter, a lens of 40 feet focal length must therefore be used.
The first attempts in solar photography appear to have been made in
France, in 1845, and the solar prominences were daguerrotyped in 1851;
but it was not until 1860, that Mr. De La Rue succeeded in obtaining
some beautiful negatives of the phenomena presented in an eclipse of the
sun, and was thus enabled to determine a great astronomical problem, by
showing that the red flames, or prominences, really belonged to the sun
itself. At the present time, photographs of parts of the sun’s disc are
regularly taken at Kew, and other observatories, without the very long
and heavy telescopes, which introduced many mechanical difficulties into
the operation; for, by means of Foucault’s siderostat, the great lens and
the photographic apparatus can be used in one fixed position. The
siderostat is an instrument on which a flat mirror, made of glass worked
to a perfect plane and silvered externally, is caused by clockwork to follow
the motion of the sun, so that the reflected beams can be projected in any
required direction unchangeably, and, therefore the image of the sun (or
other heavenly bodies) viewed in the mirror, is absolutely stationary. The
lens, carried in a short tube, has its axis directed to this image, just as it
would be pointed at the luminary itself. In solar photography, the
exposure is made through a very narrow slit in an opaque screen, which
is caused to move rapidly in front of the image. Very fair photographic
images of the sun, of several inches diameter, can, however, be obtained
with an ordinary telescope of five feet or so focal length, by substituting a
small photographic lens and camera in the eye-piece, and by enlarging
the image in printing.
As early as 1840, Dr. Draper succeeded in daguerrotyping the moon,
but it was not until 1851, that lunar photographs, obtained by Professor
Bond, another American astronomer, were first exhibited in England.
Many other distinguished experimenters have since successfully turned
their attention to this subject, such as Dancer, of Manchester, Secchi,
Crookes, Huggins, Phillips, and De La Rue. The latter, and also Mr.
Fry, by photographing the moon, at different periods of her libration,
have obtained very beautiful and interesting stereoscopic prints of our
satellite, in which she presents to the eye the roundness and solidity of
a cannon ball. Mr. Rutherford, in America, had an object glass of 11¼
inches diameter, made expressly with correction for the chemical rays,
and with this instrument he has produced some of the finest photographs
of the moon that have yet been taken. Reflecting telescopes, which
have the advantage of uniting all the rays in one focus, have been used
with excellent results, and it is said that some taken with the great
reflector at Melbourne, where also the atmospheric conditions are very
favourable, are almost perfect.
Excellent photographs of the planets have also been taken by Mr.
Common and others; but they are of course small, and have contributed
625so far, much less to our astronomical knowledge than those already
mentioned. Very different are the results obtained in what, a short time
ago, appeared a less promising field. The image of a so-called fixed star,
in even the most powerful telescopes, presents itself as a mere luminous
point, and this is the case whether the star is one of the brightest or one
of the least conspicuous. The telescopic appearance is simply a more
or less brilliant point. The various degrees of brightness which distinguish
one star from another (stella enim a stellâ differt in
claritate), and which the unassisted eye attributes to difference of size,
led, long before the invention of telescopes, to a classification of them
accordingly. The brightest stars are said to be of the 1st “magnitude,”
those of the next inferior degree of brilliancy, of the 2nd “magnitude,”
and so on, down to the 6th, which includes the faintest star discernible
by an acute eye under favourable circumstances. But stars too faint to be
thus seen came into view in the field of the telescope, and therefore those
of the 7th magnitude, and beyond, are termed telescopic stars, and each
additional power given to the instrument brings others in view that
previously were invisible. The classification has been carried down to the
18th or 20th magnitude, which expresses the limit of visibility with the
most powerful telescopes yet constructed. In the methods hitherto
employed for this classification, there is necessarily much that is arbitrary
and vague, and it is quite common to find a different magnitude assigned
to the same star by different authorities. Now the photographic plate
enables the astronomer to determine the relative brightness of stars
quite definitely. Everyone knows that the time required to impress an
image on the sensitive plate is longer, as that image is less luminous.
Hence, by finding the time required for the images of different stars to be
impressed, we have a measure of their relative luminosities. Suppose the
image of a group of stars is allowed to act on a plate for, say, 5 seconds,
we should find only the brightest stars represented. If a second plate
have double the exposure given, it would be impressed by the images of
not only the brightest stars of the group, but also by those of the next
degree of brilliancy; and a third plate exposed for 20 seconds would
show more stars than the two former exposures. So that plate after
plate might be exposed under the same group for successively longer and
longer intervals indefinitely. Exposures extending over hours have
been made, notably by Mr. Common in England, and by Mr. Gill at the
Cape of Good Hope, showing not only how magnitude may be determined
to any extent, and the heavens most accurately mapped out, but
with this very remarkable result:—thousands of stars, invisible even in
the most powerful telescopes, are portrayed in the photographs. Let us
consider for a moment the significance of this fact with regard to the new
space-exploring powers it has placed in the hands of science. The
number of stars visible to the unassisted eye in the whole expanse of the
heavens has been variously estimated, but the figures usually given lie
between 3,000 and 4,000, and the highest estimate for the most acute eyesight,
under the most favourable atmospheric conditions, places the limit
at 5,000. The brightest star in the heavens is Sirius, and Sir. J. Herschel
ascertained that its light is about 324, that of an average star of the 6th
magnitude. Taking the average luminosities of stars of the first six
magnitudes, Sir W. Herschel, from his own observations, represents their
relative brightness by the following figures: 100; 25; 12; 6; 2; 1. The
different degrees of brightness seen is, probably, due to the following
626three causes, combined in various proportions: (1) the different sizes of
these luminaries themselves; (2) differences in their intrinsic luminosity;
and, (3) differences in their distances from us. And it is also extremely
probable that the last is generally by far the largest factor of the three.
It has been found by photometrical experiments, that the light we receive
from the sun is 20,000,000,000 (twenty thousand million) times more than
that of Sirius. If we suppose Sirius to be in reality only as large and as
bright as our sun, it follows that its distance from us must be no less than
13,433,000,000,000 miles. The distance of stars of the 16th magnitude
has been estimated to be such that their light—travelling at the rate of
185,000 miles per second—takes between five and six thousand years to
reach us. For a long time no sensible parallax could be discovered in
any of the fixed stars; that is, no change in their positions was discernible
when viewed from points 183,000,000 miles apart, namely from the
extremities of a diameter of the earth’s orbit. In other words, if we suppose
the line of the length just mentioned to form the base of a triangle, having a
star at its vertex, the angle formed by the sides is so small that the most refined
instruments failed to measure it. In recent times, however, the parallax
of a few stars—about a dozen or so—has been detected and approximately
measured. The greatest observed parallax belongs to in α the constellation
of the Centaur, a star of the first magnitude, 30° from the south pole
of the heavens, and of this the parallax amounts to but a little more than
nine-tenths of a second of angular measurement, corresponding with a
distance of nearly 20,000,000,000,000 miles, a space which takes light
3½ years to pass over. This star is, therefore, believed to be the nearest
of any to our system. The smallest parallax that has been measured in
any of these few stars is a fraction of a second of angle corresponding
with a distance twenty times greater than the other, and requiring seventy
years for light to traverse it. Now, as the photographic plate shows us
stars of magnitudes indefinitely smaller even than the telescopic sixteenth,
we cannot but marvel at the manner in which the light travelling from
these suns in the immeasurable depths of space, and taking untold
thousands (nay, millions, it may be) of years in its journey is yet able so
to agitate the atoms of our silver compounds that images of things that
will themselves, probably, never be seen by mortal eyes are presented to
our view. A circumstance requiring explanation will occur to the reader’s
mind in connection with stellar photography; and that is, how does it
happen that, if the image of a star is a mere point, it nevertheless impresses
the plate as a visible dot? It is probably because the point is a
centre whence the photographic influence radiates laterally on the plate
to a small but yet sensible distance.
Among the cosmic objects presented to our observation there are none
more fully charged with interest and instruction than the Nebulæ. These
are faintly luminous patches, in some few cases visible to the naked eye,
but for the most part telescopic. The milky way, which extends round
the celestial sphere, is a very conspicuous phenomenon of the same kind.
A few other hazy, cloudlike patches are seen in various parts of the
heavens, visible on a clear moonless night when the eye is directed
towards the proper quarter. The well known group of the Pleiades
sometimes presents this appearance, but most persons are able by the
unassisted vision to discern in it a group of six stars at least, and an
opera-glass or ordinary hand telescope easily resolves the object into a
cluster of 20 or 30 distinct stars. Telescopes of higher powers bring
627more stars into view, and as many as 118 have been counted in the group.
There are several other groups of this kind perceptible to the naked eyes
merely as diffused patches of light, but resolvable by the telescope into
thickly clustered groups of minute stars; but in many of the resolvable
nebulæ the separate stars appear spread on a back-ground of diffused
luminosity. Again, there are other nebulæ which telescopes of the highest
powers we possess fail to resolve at all. Not only has the photographic
method shown stellar components of some of these last, but it has
depicted the form of nebulæ never seen at all, and whose existence was
previously unknown and unsuspected. For example, the photograph has
revealed the existence of a back-ground of nebulous patches to the stars
of the Pleiades—a thing that had never before been suspected, although
the group has been repeatedly observed by the most powerful telescopes.
Those who are at all acquainted with astronomy, will understand the
significance of this discovery for the science. The results already obtained
afford a marvellous support to the famous speculation known as the
nebular hypothesis. And as the forms of these objects are accurately
shown for us by their own light, changes in their appearance may thus
be detected as time goes on which may serve to lift the above named
theory into the region of demonstrated truth. The nebulæ which neither
telescope nor camera can resolve are such as the spectroscope proves to
be masses of glowing gas or vapour.
It has been already mentioned that the light from these immeasurably
distant stars and nebulæ is so faint that the most sensitive photographic
plates have to be exposed for hours. This would be a matter of no
difficulty if the clockwork mechanism by which the apparatus is made to
follow the apparent motion of the heavens could be constructed with
absolute perfection. But as this is not obtainable, even with the most
careful workmanship, and the smallest jar or irregularity would distort
and confuse the images, this source of disturbance is eliminated in the
following manner: attached to the photographing apparatus and driven
with it is a telescope, provided with cross wires, and through this an
observer views some star during the whole period of the exposure, his
business being to keep the image of the star accurately on the cross wire,
which he is enabled to do by having the means of slightly modifying the
movement of the clockwork. In the Paris Exhibition of 1889 were
shown many very fine large photographic prints of nebulæ (notably of
great nebula in Orion), which have recently been obtained in this manner,
and those nebulæ that had been photographically resolved had the stellar
components marked with wonderful distinctness. Comets and meteorites
have been photographed, and even the aurora borealis and the lightning’s
path have been brought within the camera’s ken.
Space would fail us to describe the many applications now found for
photography in microscopy, in medicine and surgery, in anthropology,
in commerce, and in the arts. It is obvious also from the improvements
that are continually made, that many of these applications have not yet
received their full developments. Photography has been enlisted into
the service of the army and navy, and regular courses of instruction in
the art are given in their training schools. A well equipped photographic
waggon now accompanies every army corps, and in almost every ship of
war, some proficient operator is to be found. By an ingenious combination
of photography, aerostatics and electricity, it is possible to
obtain with perfect safety accurate information of the disposition of an
628enemy’s forces and fortifications. A small captive balloon is sent
up, to which is attached a camera. At a height of a few hundred yards,
the balloon is practically safe from any projectiles, and in its cable are
interwoven two electric wires by which currents are conveyed to electro-magnets,
which produce all the movements required for any number of
exposures. Jurisprudence has found its account in recognizing the art, for
the photograph is received in evidence for proving identity, etc. The
administration of the criminal law takes advantage of the art to secure
the likeness of prisoners for future identification, and the modern instantaneous
process renders unnecessary the subjects’ concurrence with the
operation. Again, if the “hue and cry” has to be raised for an individual
“wanted” for any offence, and a photographic likeness of him is procurable,
thousands of copies can be made of it in a few hours, by night as
easily as by day, and distributed to every police station in the whole
country.
Modern processes now enable us to obtain prints from negatives in as
many seconds as a few years ago hours were required, and this by artificial
light. A process of printing lately introduced and yielding artistic results
which deserve to find more general favour, is that called the platinotype.
Instead of the ordinary print produced on lightly glazed paper by the
reduction of silver compounds, and of questionable permanency, the
image is formed in the paper by metallic platinum, the most changeless
of all possible substances under ordinary influences. The pictures are
of a rich velvety black, with soft gradations, and the surface is without
glaze or glare. The print has, in fact, the appearance and all the best
qualities of the most highly finished mezzotint engraving, combined with
the minute fidelity characteristic of the photograph. The problem of
producing a photograph in colours, permanently showing nature’s tints in
all their gradations, has still a great fascination for some experimenters,
and startling announcements are made from time to time of some discovery
in this direction. It does not appear, however, that any success has
really been arrived at, beyond the results long ago obtained by Becquerel
as described on page 614; and, indeed, as our knowledge of the science
of the subject increases, the less likely does the possibility of photographing
colours appear. It is, however, never safe to lay down the limits of
discovery in science.[14] Note that precisely in the matter of rendering
colour even in its due gradation of tone or luminous intensity, the photograph
is quite untruthful. Everybody has noticed how unnaturally dark
and heavy the foliage of trees appears in the prints; if we suppose a lady
in a blue dress, with yellow trimmings, to sit for her portrait, the photograph
will show her in a white dress with black trimmings; a sitter with light
yellow or auburn hair will appear of quite a dark complexion; if you
photograph a lemon and a plum together, the latter will probably
come out lighter than the former; or if a daffodil be the subject, the
flower will be drawn in tones much darker than the leaves. This incorrectness
of tone relations can, however, be greatly lessened by the
device of reducing the quantity of the blue rays, by interposing a piece of
optically plane yellow-tinted glass, by using the sensitive plates tinted
with certain coal-tar dyes, which are now prepared and sold under the
name of “ortho-chromatic plates,” or by both methods combined.
If any illustration were needed of the great popularity now attained by
the practice of photography, reference might be made to the large number
of periodicals devoted to the subject, and appearing weekly, fortnightly,
629quarterly or annually, in every civilised country, and also to the multitudes
of societies that have been formed for the promotion of the art. In Great
Britain alone there are now at least 150 such societies in active operation,
and they are correspondingly numerous elsewhere. If, when we consider
all that has been accomplished up to the present time, with the jubilee
year of photography scarcely passed, and observe the increasing numbers
of its cultivators guided by the explanations of its phenomena that science
is beginning to furnish, we can expect a corresponding progress in the
next fifty years, then the centenary may be reached with a roll of achievements
that could we know them now we should think marvellous.
As already remarked elsewhere, the practical side of photography has
outstripped the theoretical one, for so far its progress has been much less
indebted for processes and technic to the direct guidance of science
than almost any other of our Nineteenth Century acquisitions, such as
telegraphy, electric lighting, etc. The materials employed, and the mode
of manipulation, have certainly not been deduced from previous knowledge
of the nature of light or from the laws of chemistry, although when, by
repeated trials and happy guesses, the right direction had been found, the
field into which it led could be more easily explored under the direction
of chemistry and physics. But even yet the fundamental principle, or the
precise nature of the action of light on certain compounds, has not been
definitely made out, and although some theories on the subject have been
proposed, no one has been generally accepted as an adequate explanation
of the known facts, and still less have any quantitative relations been
established for these actions. The photographer cannot compose a
formula for the composition of his emulsions and developers from assured
data like those that enable the chemist to weigh out with accuracy the
constituents that go to produce a required compound.
The attainment of permanency in its products, which, by several processes,
photography can now boast of, is one of its triumphs, and will tend
greatly to enlarge the sphere of its utility. For example, we have a public
institution, known as the National Portrait Gallery, in which it is sought
to gather together and preserve the likenesses of the most eminent
Englishmen, and presentments of such of far less fidelity than photographic
portraits are eagerly sought after. It has been suggested that
something like a National Gallery of permanent photographic portraits of
the chief men of their time would be a fitting and acceptable legacy to
the public of the future. This idea has much to recommend it, particularly
as authentic likenesses would thus be secured for the nation beyond
the chance of loss.
Photography has been applied in preparing blocks in relief for printing
along with letterpress in the same way as woodcut blocks. The process
has the great advantage of producing in a wonderfully short time a perfect
facsimile of the artist’s drawing without the intervention of any engraver.
A plate of zinc, brass, or copper, coated with a dried film of bichromated
albumen, is exposed to light under the transparent negative of a drawing
in pure line, that is, one having in it only lines of uniform colour throughout.
The parts of the film reached by the light, which correspond with
the lines of the original design, are rendered insoluble, while the rest can
readily be removed by water. These unprotected parts have then to be
removed by the action of acids, but these are used alternately with the
application to the plate of certain compositions, the purpose of which is
to prevent lateral erosion of the lines in relief before the requisite depth
630of the metal has been removed. Fig. 147f is the reproduction of a pen-and-ink
sketch by this or some similar process. But nature and the
ordinary photograph show us graduated tones which ordinary printers’
ink cannot really reproduce, inasmuch as it is incapable of gradation, and
can give the effect of gradation only by such devices as are mentioned on
page 642 (last sentence). Now, the photograph cannot yield a printing-block
until its continuous tones are broken up into lines or dots. Not a
few methods of doing this have been contrived, but that which is by far
the most commonly used, and is most successfully practised on the commercial
scale, is simple in principle, although in actual working it calls for
much experience and skill. The negative is taken upon a wet collodion
plate, in front of which, within the camera, and at a very short distance
(say 1 30th inch) from the film, is a transparent screen, bearing two sets of
parallel opaque lines at right angles to each other. These lines are
mechanically ruled with the utmost regularity, and are separated by only
very small intervals. There may be from 80 to 200 of them in the space
of one inch, according to the class of work required. The effect of this
is that the light reaches the photographic film through a series of minute
transparent squares, the sides of which may be only from the 1 140th to the
1 400th of an inch in length. Now it is found that the brighter lights from
the original positive, after passing these small apertures, spread so as to
more or less cover the opposite parts of the negative, while the feebler
lights, from the shades of the original, impress the plate to a less degree,
the developed image in these showing, perhaps, merely a small dot or,
in the very darkest parts, a blank. In this way, then, may the photographic
negative be obtained with a granulated texture following in
graduation the tones of the original. After this, the rest is easy, for the
process of exposing a metal plate, coated with a sensitive film under the
negative, and of etching it with acids, etc., is essentially the same as in
the foregoing. Such is the half-tone process, which is now so largely
superseding wood and other engraving. It is unnecessary to describe
technical details here, such as the employment of bitumen of Judæa as
the coating for the metal plate, or how the image must be reflected into
the lens from a mirror to avoid a reversal in the final print, etc. There
are endless modifications of the processes briefly mentioned above, and
some of these are guarded as valuable trade secrets. Several of the illustrations
in this work are prepared by the half-tone process, of which plates
I., IV., V., etc., are examples, and they should be examined with a strong
lens, in order that the different rendering of the light and the dark parts
may be compared.
It is the statement as to the futility of assigning limits to scientific discovery
that has been justified by facts. The preceding edition of this
work was not long in the hands of its readers before the solution of the
problem of photography in colours was announced from Paris, where, at
the close of 1890, the physicist M. Lippmann had succeeded in photographing
the solar spectrum in its natural colours, and at the beginning
of 1891, he was able to exhibit at the Academy of Science untouched
photographs of a stained glass window in three colours, of a dish of
oranges and red flowers, and of a gorgeously coloured parrot, all in their
631natural tints. The method employed had no apparent relation to that of
Becquerel, but was of the simplest, and, moreover, one which any reader
who has followed the first few pages of our section on the “Causes of
Light and Colours” will have little difficulty in completely understanding,
if he has devoted a little attention to Fresnel’s interference experiment.
M. Lippmann took a photographic plate, coated to a greater depth than
usual with a gelatine film containing the sensitive salts of silver, and in
the camera this plate was exposed with the glass towards the lens, while
at the other side of the film was a metallic reflecting surface, namely,
quicksilver. Supposing a ray of red light to enter the glass and traverse
the film, it would be reflected from the metallic surface, and would meet
the direct ray within the substance of the film, with a difference of length
of path that would produce the interferences already described, and so give
rise to alternate lines or bands of darkness and brightness. It would, of
course, be in the lines of maximum brightness that the silver would be
first deposited by the photographic action, and these microscopically fine
lines or striæ of silver would give back, from ordinary light, a colour corresponding
to the waves of red light that produced them. Similarly with
the other colours. Anyone may observe the production of colour from
ordinary white light in the iridescent tints of mother-of-pearl, where the
effects are due to the varying distances of fine edges of the layers of the
substance. If an impression is taken from a piece of mother-of-pearl by
solid paraffin, or by white wax, or even by common red sealing-wax, the
colours will seem to be adhering to the impression, but the operation may
be repeated times without number. It is the distance apart of the lines
or striæ that determinates the colour, and this is always some definite
multiple of the wave lengths, given on p. 411, for the various colours. M.
Lippmann’s products are true colour photographs, and they form a new
and elegant experimental demonstration of the doctrine of luminiferous
undulations.
The colour effects of nature have also been reproduced by taking photographs
of the same scene through coloured glass. Thus a screen of
yellow glass will intercept the blue and the red rays, and the sensitive film
will be impressed with images of objects containing yellow rays only, and
that in proportion to the quantity of these rays that enter into any given
tint. Similarly with images taken through red and blue glasses. The
positives from these partial images being projected by three optical lanterns
on the same space on a screen, and each being coloured by passing
through tinted glasses like the original, the superposed images thus combined
give a very lively impression of the natural colours in all their
gradations.
Among the many processes for reproducing photographs by non-photographic
processes, some have been more or less successfully combined
with colour printing. Some of these productions are very effective,
and are more attractive to many persons than the monochromatic tints of
ordinary photographs.
632
Fig. 312.—Portrait of Aloysius Senefelder.
PRINTING PROCESSES. — STEREOTYPING. — LITHOGRAPHY. — OTHER PROCESSES. — THE LINOTYPE MACHINE.
As it is beyond contradiction that printing is one of those inventions
which have most influenced the progress of mankind, so it will be
admitted that certain modern processes, by greatly facilitating the operations,
and vastly extending the resources, of the art, possess an interest and
importance surpassed by few of the subjects we have discussed. In a
former article the reader has been made acquainted with the steam printing-press
and other applications of machinery by which the impressions of a
form of type, or of a pattern, can be rapidly multiplied. Here we have to
describe some ingenious methods of preparing the forms or originals for
letterpress and other printing, and certain beautiful processes for multiplying
drawings, engravings, and pictures.
This term is applied to the process of obtaining the impression of a
form of movable types, or of a woodcut, on a plate of metal which
can be printed from. These plates, after the required number of copies
633have been printed, can be stored away; and they are ready for use whenever
another issue of the work is required. When the pages that are to
be stereotyped have been set up in ordinary type, there are several methods
by which the stereotype plates may be obtained from them; or rather,
there are several materials used to form the matrix or mould in which the
metal is cast. When plaster of Paris is used, the form is first slightly
oiled, to prevent adhesion of the plaster; a thin mixture of plaster and
water is then poured upon the form, which is surrounded by a raised rim,
to retain the plaster. The thin plaster is carefully led into all the recesses
of the type, and then some thicker material is poured on. The plaster
soon sets, and is lifted off the type, and, after drying, is ready to receive
the molten metal of which the stereotype plate is formed. This metal is
an easily fusible alloy of lead, antimony, and other metals, which takes the
form of the mould with great accuracy, and is, when solid, sufficiently hard
to print from.
Fig. 313.—Press for Stereotyping by Clay Process.
Another plan is to make use of prepared clay, spread upon an iron plate,
for the formation of the mould. The face of the type is brushed with benzine,
the plate with the clay is laid upon it, and pressure is applied. The
whole is then dried in a slow oven, and the clay, when detached from the
type, is ready to form the mould. The advantages of the clay process are
that the type does not require to be afterwards cleaned from oil, and that
the material does not fill up the deeper spaces of the form, so that a thinner
stratum of metal suffices to form the stereotype plate.
A third mode of obtaining the mould has been already mentioned in
connection with the Walter Printing Press (page 313), in the working of
which the papier maché process is ingeniously made to supply the curved
stereotype plates for the cylinders. This process is also largely used for
other newspaper presses, and sometimes for bookwork, as it forms an invaluable
means of expeditiously obtaining a number of stereotype plates from
the movable types. This production of a number of similar forms makes
it possible to strike off a very large number of copies in a short time, for
many presses can be employed simultaneously. For the paper process a
634number of sheets of tissue-paper are pasted together, and the moist paper
is laid upon the form; then the operator, by light strokes of a brush, beats
down the paper into the hollows of the type, beginning at the centre of
the page, and going towards the margins. A sheet of stout unsized paper,
called “plate paper,” constitutes the upper layer; and when the whole has
been well beaten down upon the type, pressure is applied by means of a
screw acting upon a plate of iron covering the whole. In this condition
a gentle heat, produced by steam, is made to completely dry and harden
the paper matrix, which is very soon fit to be used for casting the metal.
The apparatus for this purpose consists of a hollow iron table, within which
steam is made to circulate. On this the form is placed, and the platen is
pressed down upon it by means of a screw. In many cases the platen also
is heated by steam, to accelerate still further the drying of the matrix,
which is effected in about four or five minutes. One paper matrix, by careful
use, will serve for the production of a series of casts without receiving any
damage from the molten metal, as this is fusible at a low temperature.
The mould for casting flat stereotype plates from the paper matrix is
made of iron, and has parallel surfaces, which admit of being so adjusted
that the thickness required in the plates may be obtained very nearly.
The paper matrix is laid on the horizontal iron bed of the mould; gauge-bars
are adjusted, which retain it in its position; and then the second plate
is folded down—the distance between that and the paper being determined
by the gauge-bars. The cover is secured by clamping-screws, and then
the mould is turned upright to receive the metal, which is removed, when
solid, after the mould has been turned back into its horizontal position.
However the stereotype plates have been produced, it is necessary accurately
to adjust their thickness by planing off some of the material from
the back. The edges have also to be cut and trimmed to the exact dimensions
required by the press. Various machines have been devised for
effecting all these operations with accuracy and dispatch. The plates are
afterwards mounted on wooden or metal blocks to bring them to the
height of ordinary type.
A fourth method of producing plates for the same purpose as the stereotype
plates already described is by electrotyping. This method appears to
have been introduced as early as 1840, but the first results were not without
imperfections. Now, however, this plan is almost universally applied
to bookwork and woodcut illustrations. Many of our popular illustrated
periodicals have so large a circulation that the wooden blocks would necessarily
be spoiled by being used in steam presses long before they had
yielded the required number of impressions; and the method has also the
great advantage of securing the original engraving from the chance of accidental
damage, by which a block is sometimes irretrievably injured. Hence
woodcut illustrations are now always printed from electrotype copies of the
engraved blocks, whether the work itself be printed from movable type or
not. But the electrotype or stereotype process is always resorted to in the
case of a work, whether illustrated or not, when it is foreseen that a re-issue
will be demanded. These processes are also of great advantage to the
practical printer, because when the pages set up in type have received
their final corrections, he can take the casts, and then the type may be distributed—that
is, returned to the cases ready for the compositors to use for
other work.
The electrotype process is almost as simple as those for producing
stereotype plates by casting, and its productions excel these by their great
635durability and extreme exactness of reproduction. We may take it for
granted that the reader is familiar with the fact that ordinary letterpress
characters and woodcuts are printed from forms, in which the black portions
are in relief. For woodcuts the artist makes the drawing, in reversed
position, on a block of finely-grained boxwood, in which the fibres of the
wood are perpendicular to the surface. The engraver hollows out all the
parts which in the impression remain white, while all the parts which are
to receive the ink and produce the black parts of the impression must be
left at the original level. The wooden blocks thus engraved would serve
to produce a certain number of impressions, which could be taken off by
careful hand-printing without perceptible damage to the block. But the
pressure necessary for printing inevitably crushes the projecting parts of
the block; and the impressions, after a certain number, lose their sharpness.
This is especially the case in machine printing; but not only does the
electrotype cast present a surface capable of bearing hard usage much
better than those of the hardest wood, but even if the number of impressions
required should wear out the metal plate, it can easily be replaced by
another cast from the original block.
The mould which serves to give the electrotype cast may be made either
of gutta-percha softened by a gentle heat and applied to the wood, or of
wax. In either case a powerful pressure is applied, in order to force the
yielding substance to take the forms of the engraved block or of the metal
type. Wax is now generally preferred; the yellow wax used for this purpose
is melted, and poured into a shallow pan; when it has become solid,
it is sprinkled over with finely-powdered pure blacklead, which is brushed
over the surface, and then the excess is removed by blowing with bellows
made for the purpose. Thus prepared, the wax is placed over the type-form
or wooden block in a powerful press, sometimes worked by hydraulic
power; but more frequently a toggle press is employed, in which the pressure
is given by a screw and crank-wheel acting on two elbow joints, or
toggles. For the information of non-mechanical readers it may be stated
that a “toggle” consists of two bars jointed together, and placed nearly in
a straight line: when a pressure is applied to the joint, tending to bring
the rods still more nearly into a straight line, their extremities are thrust
apart with a great force, which increases indefinitely as the rectilinear position
is approached. In the electrotyper’s press there are two toggles constructed
of very broad bars, or rather thick plates, for they have nearly the
width of the bed of the press. With this machine a very powerful and
regular pressure is applied; and the wax in a few minutes takes a sharp
impression, embracing all the most delicate details of the work, and becomes
at the same time very hard. The impression, of course, has hollows
corresponding to the projections of the wooden block or type-form, and
vice versâ. The face of the wax mould is now very carefully and completely
blackleaded, a soft brush being used in the process. It is then
placed in the solution of sulphate of copper, and the blacklead receives a
deposit of copper, in the manner explained in a former page (498). In
about forty or fifty hours a firm, compact deposit, about as thick as the
finger-nail, covers the blackleaded surface, forming a perfect reproduction
of even the most minute details of the engraved block or letterpress form.
The next operation has for its object the removal of the thin shell of
copper from the wax. This is effected by exposing the mould to a gentle
heat by immersing it in hot water, or by placing it on a hollow iron table
which is heated by steam. The wax is run off into a proper receptacle for
636future use, and any portion adhering to the copper is removed by the action
of naphtha or of a solution of potash. The thin copper shell is then tinned
on the back, and an alloy of lead with some tin and antimony, forming the
backing metal, is poured on it, to the depth of about one-eighth of an inch.
When this has become solid the backing is planed, so that the compound
plate may have a certain regular thickness, and that the back surface may
be parallel to the face. The edges are cut by a circular saw and trimmed by
machine-tools, and the plate is rendered perfectly even, and adjusted with
the greatest possible exactness to the required thickness. It is prepared
for the press by being screwed down upon a block of wood of a certain
thickness, so that the face of the plate may have the same height as common
type, the screws passing through the margin or other hollow parts of the
face of the cast. No more enduring surface than the copper of these electrotype
casts, backed up by the hard alloy, has yet been discovered.
To Aloysius Senefelder, a musician attached to one of the theatres in
Munich, whose portrait appears at the head of this article, is due the
invention of the art of lithography. It is said he used to arrange his
musical compositions on a kind of slates, formed of flakes of the limestone
which is found in the neighbourhood of Munich. One day a memorandum
which he had made in this manner happened to fall into a slop-bucket
full of greasy water; on withdrawing the piece of stone, he noticed with
surprise that the grease had attached itself to the characters, while the
rest of the stone remained quite clean. Such an incident might have happened
to each one of a thousand men, and its significance might not be
perceived; but it suggested great possibilities to Senefelder, who, applying
himself for some years with ingenuity and perseverance to experiments
with the Munich limestone, became, in the year 1800, the inventor of a new
art. Though he was no chemist, and was unskilled in mechanics and in
drawing, yet within four years from his first observation he had succeeded
in finding the proper materials for his crayons and the appropriate acids
for acting on the stone, in contriving a suitable press for taking the impressions,
and in producing samples of lithographic work in various styles of art.
He endeavoured to keep his processes secret, and having obtained the
exclusive right of exercising his invention in his own country, he attempted
to carry on all the operations himself. Little by little, however, the general
nature of the process became known, and although the details were jealously
concealed, ingenious persons in France and elsewhere, by force of
experiment, succeeded in re-inventing the art for themselves, and Senefelder
never profited by his invention as he should have done.
The first lithographic press in London was established by Mr. Hullmandel
in 1810. The value of lithography as a means of multiplying works of art
was soon afterwards proved by the publication of a magnificent series of
picturesque delineations of the quaint architecture of the old towns of
Flanders and Germany, drawn on the stone by Samuel Prout. The late
Mr. J. D. Harding largely contributed to the popularity of lithography by
the landscapes which he drew on the stone, and thus placed in the hands
637of every one, prints in which all the freedom and force of the artist’s work
were secured. The French designers excel in fine-art lithography, and
many beautiful productions of their crayons have been published in every
department of pictorial illustration.
The best lithographic stones come from Germany; but for some kinds
of work stones from other localities are used, on account of their less cost.
Thus, in England, a stone yielded by the white lias formation near Bath
has been found to possess the requisite qualities. The stones for lithography
are prepared in much the same way as slabs of marble are polished;
that is to say, by rubbing one slab against another with sand and water.
When the stones have thus been brought to a plane surface, they are finished
according to the purpose for which they are intended. If they are intended
to receive written characters, they are polished to a very smooth surface
by means of pumice-stone. But if they are to take drawings, then a certain
uniform grain is given by means of finely-sifted sand, the operation
being performed in a similar manner to that in which the stones are dressed,
only pressure is not applied to the upper stone. The stones, after being
washed and dried, are carefully covered on their prepared surfaces with
thin paper, and are sent out for use.
When the stone is employed to reproduce written characters, or drawings
imitating those done with a pen, lithographic ink is made use of with an
ordinary pen, a ruling-pen, a fine brush, or a pen which the lithographer
makes for the occasion out of thin metallic plates. The composition of the
ink varies much: the usual ingredients are wax, gum-mastic, gum-lac, soap,
and lampblack. This composition forms a solid, which is rubbed down
with water to a thick liquid when required for use. The characters have,
of course, to be written on the stone in a reversed position, and the lithographer
acquires the habit of doing this with neatness and dexterity. He
is provided with a looking-glass for viewing his work, in order to see the
effect which will be given by the impression, for the looking-glass shows
the characters in their usual position, just as the image of ordinary writing
seen in it is reversed, showing, in fact, the very appearance the characters
present on the stone. For a drawing, a lithographic crayon is used, made of
wax, soap, grease, lampblack, and other ingredients. With this the drawing
is made on the stone exactly as on paper, save the necessary reversals.
When the design has been placed on the stone, a liquid containing nitric
acid and gum is poured over it. This liquid acts on all the parts of the
stone not protected by the ink or crayon: they are thus rendered incapable
of receiving printing-ink, while the protected parts have the impression
more strongly fixed; for when the stone has been well washed with water,
and turpentine has afterwards been applied, so that all the matter used in
marking the design is dissolved away, the seemingly obliterated characters
reappear when—after the stone has been lightly wiped with a damp
sponge—the roller charged with printer’s ink is applied. The ink is taken
up by the stone only at those places which have not been acted on by the
acid. The impression is obtained by laying a sheet of damp paper on the
inked stone and applying pressure by means of a roller, under which the
stone passes. The stone is moistened with water after each impression
before the inking-roller is again applied.
The lithographic stone, like other originals used in printing, is liable to
deteriorate when large numbers of impressions are taken from it. This
would be a serious drawback in lithography, but for a method of renewing
the impression, which renders it unnecessary for the artist to retouch his
638work. This is the process of transferring, which is practised by the aid of
a certain kind of paper specially prepared by a coating of paste. On this
a proof is taken from the original drawing on the stone, and the still moist
sheet is then applied to another stone, with the face downwards, and passed
under the press. The effect of the pressure is to cause the adherence of
the layer of paste to the stone; and when the paper has been thoroughly
wetted at the back, it may be removed, leaving the paste still adhering to
the stone, with the impression beneath it. When water is applied, the paste
is washed off, while the ink of the impression remains attached to the
stone, there reproducing the design drawn on the first stone. The transferred
design is treated in exactly the same manner as the original drawing,
acid being poured over the stone, &c., and the impressions obtained by
the same method of successively sponging, inking, and pressing. The
transferred drawing may be made to yield another transfer, and so on indefinitely;
but when a large number of impressions from one design are required,
it is usual to make at once from the original as many transfers to
separate stones as will yield the required number of impressions without
deterioration. In this way as many as 70,000 copies have been taken from
a single drawing without their showing any marked difference in the character
of the impressions.
The transfer process is also applied to place on the stone characters which
have been written with a pen in the ordinary manner on prepared paper.
In this way a person’s handwriting is so accurately reproduced in the impressions
that it is often very difficult to detect the interposition of the
lithographic stone, and the impression often passes as the immediate production
of the writer’s pen. It is obvious that drawings etched with the
pen on transfer-paper can be printed from in the same manner. And line
engravings, which have been originally produced by cutting hollow lines on
polished plates of copper, can be printed lithographically by transferring
an impression to the stone. By transfer also the impressions of raised
types or of woodcuts can be printed from the stone when desirable.
A beautiful and important application of lithography to the reproduction
of pictures in colours has been so successfully carried out that a new
branch of the art, termed chromo-lithography, now gives facsimiles of
water-colour drawings and of paintings in oil. The copies of water-colour
drawings especially are remarkable for their artistic qualities, and it is
undeniable that these cheap reproductions of good paintings have done
much to extend the knowledge of art. It is not contended that a chromo-lithograph,
for example, after one of old William Hunt’s rustic figures, or
birds’ nests with banks of primroses, can possess the wonderful refinement
of the original; but it will nevertheless convey much of the artist’s sentiment.
Such transcripts of the works of our best artists adorn the homes of
thousands who have never perhaps had the opportunity of even seeing the
painter’s original handiwork. In many a remote settlement in distant
colonies, as in many an English home, the chromo-lithograph is the
brightest of the household art treasures.
The principle of chromo-lithography consists in printing on the same
paper with inks of various colours from different stones successively, so as
to produce, by the juxtaposition and superposition of the various tints, the
effect of a coloured drawing or painting. The artistic effects of the best
chromo-lithographs require a great number of printings for their production,
in some cases as many as twenty different stones being employed.
The stones and colours for such productions require true artists to prepare
639them, persons who can thoroughly understand and enter into the spirit of
the original work. The first operation consists in the preparation of a
faithful but spirited outline of the original, etched on transfer-paper, from
which the outline is placed on a lithographic stone. This sketch we have
called an outline, but it is in reality something more; for it should suggest
all the markings and limits of tints which belong to the original. This
first sketch has some points marked on the margin by dots or crosses,
which serve to secure true register in the subsequent processes; that is,
the impressions of the successive tints are so placed on the press that these
points coincide in each impression.
From the first stone as many impressions of the sketch are transferred
in light ink to other stones as there are colours required in the reproduction.
To each colour a special stone is assigned, on which the lithographer,
guided by the slight impression of the sketch, draws with the ordinary
black crayon the form which that colour is to produce on the paper.
Much artistic skill and judgment are required to do this in such a manner
as to obtain a clear and harmonious final result. The gradations of the
colours, and their blendings by superposition, must be carefully regarded.
When the form and limits of each colour have been skilfully laid down
upon its own stone, the surface is acted on by the acid, it is washed, the
ink is dissolved off by turpentine, the stone is sponged, and the roller
charged with ink of the appropriate tint is passed over it. The ink, as
before, adheres only to the parts over which the crayon has passed, and
an impression may be drawn off. Each of the other stones is similarly
treated, and when the whole are ready, a proof is taken by giving the same
sheet of paper the whole series of impressions in their proper order and
colours, with the greatest possible accuracy of register. If any alterations
appear desirable, they are made accordingly, by aid of certain devices
which need not be here described, and when a satisfactory result has been
obtained, the printing of the whole series of impressions is proceeded with.
When the number of these is very large, transfers of each stone are taken
as in ordinary lithography, only with certain extra precautions for obtaining
precision in the register.
The brilliant effects produced by using gold and silver in lithography
are obtained by using a kind of varnish, instead of coloured ink, for printing
those parts where the metal is to appear. When this varnish has
acquired a certain stickiness by partial drying, powdered gold or silver is
applied, and this attaches itself only to the varnish; when the sheet is dry
it is passed under a burnished steel roller, the pressure of which imparts a
brilliant lustre to the metal.
A method of colour-printing, in some respects resembling that of chromo-lithography,
is practised by printing in variously coloured inks from a
series of wooden blocks. This admits of far greater expedition in working
off the impressions than the process with stones. The gradations of the
coloured inks and powdered tints are produced in the same manner as
those of ordinary woodcuts in black and white; and when the colours are
well chosen, and care is taken to secure the accurate superposition of the
impressions, very pleasing effects can be produced by this means. The
coloured prints which are from time to time issued as supplements to the
“Illustrated London News” are produced by this process, and are no
doubt well known to the reader. Our plate of spectra, No. XVII., is an
example of another method of printing in colours.
640
In recent times a great number of printing processes have been devised,
but only a few have found their way into practical use, and some of
these have scarcely been so extensively applied as their merits appear to
deserve: either because the public demand has been insufficient to bring
these inventions into common use, or the cost of working them has been
too great. There is no doubt of their scientific success, whatever may be
their commercial value as competing with cheaper and readier methods.
We shall first describe the plan which has been termed Nature Printing.
This process is applicable only to certain objects which possess, or may
be made to assume, a flat form. It has been most successfully applied to
botanical specimens, the impressions of the leaves, flowers, and other parts
of plants being given with an accuracy and minuteness of detail which the
finest work of an engraver could never attain. In fact, the prints may be
examined with a microscope, and they then reveal the minute structure of
the object with wonderful clearness and delicacy. The notion of nature
printing originated with M. Auer, the Superintendent of the Imperial
Printing Office at Vienna; but the process was introduced into England,
with certain improvements, by Mr. H. Bradbury. Supposing the object
to be printed is a plant or the frond of a fern, it is first thoroughly dried by
being pressed between folds of blotting-paper by means of a screw-press.
The paper is changed several times, and, when necessary, the drying is
accelerated by a gentle heat. When the specimen is perfectly dry, it requires
very careful handling, for it is then generally extremely brittle. It
is laid upon a sheet of pure soft lead, the face of which has been formed
into a perfectly even surface, smooth and bright as a mirror. Mr. Bradbury
encountered some difficulties in attempting to produce a surface of this
kind, for small irregularities of the lead surface showed themselves; but
Mr. James Wood succeeded in preparing for him a machine by which the
lead is planed and polished in one operation. The object having been carefully
laid upon the bright and smooth surface of the lead, a powerful pressure
is applied by passing the plate between a pair of polished steel rollers.
The effect of this is to embed the plant in the soft metal, which thus receives
even the most delicate markings of the object. The next operation is the
careful and patient removal of the object from the plate; and as this is very
brittle, it will be easily understood that it does not in general come away
entirely, but portions will be left embedded in the metal. The skill of the
operator is shown by destroying these by means of a blowpipe-flame, without
in the least fusing the lead, which would of course ruin the impression.
When the whole has been removed, the leaden plate will have been engraved,
as it were, by the object itself; and in this state the plate will yield
impressions with ink in the same manner as an engraved copper plate. But
in the soft metal the image would soon be obliterated, and therefore a facsimile
of its impression is obtained in copper by the electrotype process.
For this end the lead is covered with a varnish, except on the face, and
thus the deposit of copper takes place only where it is required, and the
current of electricity is continued until a proper thickness of deposit has
been obtained. This electrotype has all the hollow forms of the lead plate
in relief, and it is used only for the preparation of another electrotype. For
this purpose its face is brushed over with fine, pure blacklead, in order to
641prevent the deposit from becoming incorporated with it, while the rest of
the plate is varnished. When it is placed in the electrotyping solution the
copper is deposited on the blackleaded face, and the action is continued
until the layer of metal has acquired the thickness of one-eighth of an inch.
It is then removed from the matrix, and is ready for the printer, who deals
with it in the ordinary manner of copper-plate printing, except that he uses
a softer paper, and this is forced by the pressure into the depressions in the
plate, so that the impression is really embossed on the paper. Coloured
inks are also used instead of black; for instance, to the leaves green-coloured
ink is applied, and to the stems, &c., brown ink.
Several works on certain branches of natural history have been very
appropriately illustrated in this way; among these, perhaps, no more beautiful
example is to be found than in “The Ferns of Great Britain and Ireland,”
with text by Lindley and Moore. The merits of the nature-printing
process appear to be the accuracy of outline in the flat form, and the delicacy
of detail in parts projecting from the surface. The impressions cannot
present artistic or natural shading in the objects; for the depth of
colour will be in proportion to the projection of the part, whereas in nature
the darkest shades are seen in the deepest recesses.
A copper plate, cut in the ordinary manner—as a line engraving, for
example—soon deteriorates, as the pressure applied for each impression
taken from it tends to close up the lines. It has therefore been necessary,
where a plate has to yield a large number of impressions, to make use of
steel instead of copper. But the electrotype has given the means of multiplying
indefinitely facsimiles of engraved copper plates, so that in many
cases a number of these are prepared, and used so long as they continue
to yield clear impressions, the original plates engraved by the artist only
furnishing the matrix. The mode of reproducing the plates by electrotyping
from the original engraved plates is identical with that just described for
obtaining the plates for nature printing from the leaden plates.
Another process of wider interest, and producing very beautiful results,
is known as the Woodbury printing process, from the name of its inventor.
It is a mode of photographically forming a picture in relief, from which
printing blocks are obtained in much the same manner as in the nature-printing
process. But the subject which is thus printed is a photograph;
and it is only because in the actual production of the impression on paper
the agency of light is not called into play that it is not described under the
head of photography, for it is an ingenious mode of causing the photograph
to engrave its own image on a metal plate. It is founded on a fact
which has already been noticed, namely, the insolubility of gelatine which
has been mixed with a bichromate and exposed to the action of light.
Mr. Woodbury has obtained the best results with a solution of Nelson’s
opaque gelatine, 1 oz. of which is dissolved in 5 oz. of water, and to each
ounce of the solution 15 grains of ammonium bichromate are added. When
a layer of this mixture, which is of course prepared in the dark, is exposed
to the action of light under a negative photograph, the gelatine is rendered
insoluble under those parts of the negative through which the light passes,
that is, in the parts corresponding with the dark shades in the original
object, and the depth of the layer thus rendered insoluble in each part
will depend on the relative thickness of the silver deposit in the negative
photograph. Thus, in the half-tints the insoluble layer will not be so deep
as under the parts of the negative through which the light passes without
interruption. But the differences of depth will appear when the soluble
642gelatine has been dissolved away on the side of the layer which is farther
from the negative. Hence, Mr. Woodbury spreads his layer of bichromated
gelatine on a sheet of plate-glass, previously coated with collodion,
and when the gelatine has become dry, the double film is detached from
the glass and exposed under a negative, the collodion side being uppermost
and in contact with the photograph. After exposure the film is temporarily
attached to another piece of glass, by means of a solution of India-rubber,
and is then immersed in warm water, which quickly dissolves the
soluble parts of the gelatine. Thus a counterpart in relief of the photograph
is obtained. This is allowed to dry, and the next operation consists in
obtaining an impression from it in metal: this Mr. Woodbury at first
obtained by electric deposition, but he has discovered a much more expeditious
process, which one would hardly have supposed possible before
actual trial. The dry hard gelatine is placed upon a flat, truly-surfaced steel
plate, with the collodion surface downward, a plate of soft metal is placed
upon the gelatine, and the whole is subjected to a pressure of about four
tons per square inch in a hydraulic press. In one minute a perfect impression
of the gelatine relief, down to the smallest detail, is formed in the
soft metal; and, strangely enough, the delicate sculpture which the light
has executed on the gelatine is not in the least injured, but will stamp its
image on an indefinite number of metal plates in the same manner.
The reader will understand that the impressed plate of metal now bears
a hollow sculpture representing the image of the original object from
which the negative photograph was taken, the darkest shades of the object
being represented by the deepest depressions in the plate, while the
highest lights are represented by portions of the metal at the level, or
nearly so, of the surface of the plate. From this plate the prints on paper
are obtained as follows: The plate is placed horizontally, with its impressed
face upwards, and a quantity of a certain kind of ink is placed
upon it. The composition of this ink, if ink it may be termed, is one of
the ingenious parts of this elegant process. It is made of gelatine, coloured
with some suitable transparent or semi-transparent pigments, and it is
poured on the plate in a warm and fluid state, and in quantity more than
sufficient to fill all the hollows. A sheet of paper is placed over the plate,
and a moderate pressure is applied, when the excess of ink is squeezed
out and escapes. That which remains in the hollows of the plate, becoming
set by cooling, adheres to and is removed with the paper, giving in
each part a force of tint proportional to its quantity, that is, according to
the depth of the hollow in the plate. The paper is laid aside to dry,
and although the picture has at first a certain relief, yet the gelatine ink
dries down, the picture becoming so flat that no difference of the surface
is perceptible. It will be observed that this mode of printing rests upon
a distinctly new principle—namely, the production of shades and gradations
of tints by the varying quantity of the ink laid upon the different parts of the
paper. The method is in this respect identical with that by which the water-colour
painter produces his gradations; for the colour is applied in transparent
layers, and the depth of the tint produced depends upon the mass
of the pigment laid on, and is greater or less according as the white of the
paper is more or less visible through the film of colouring matter. The
gradations of tint in wood and steel engraving and in lithographs are dependent
upon quite another principle—namely, the varying distribution of
spots, patches, or lines in black ink of uniform intensity. The Woodbury
print has all the detail and clearness of the photograph, together with a
643certain softness, produced by the transparency of the colouring matter, not
found in the ordinary photographic print. The method admits of any desired
tint being given to the prints, and these are perfectly unchangeable
by light. Thus the result is a print which secures every good quality of a
photograph without any of the unpleasant ones, such as hardness, harsh
tints, opacity, fugaciousness. The prints may be taken on plates of glass,
and they then form beautiful transparencies. Such prints constitute most
admirable slides for the magic lantern, since the semi-transparent colouring
matter, and the soft gradations, produce charming effects.
Another ingenious invention of Mr. Woodbury’s provides a means of
making the sunbeam engrave a mezzotint copper plate from a photograph.
The action of light on bichromated gelatine is here again taken advantage
of. A film is prepared similar to that used in the above-described Woodbury
process proper, but the gelatine is mixed with some powdered or
granular material, so that it may give rise to a granulated texture in the
resulting plate. This film is treated exactly in the same way as before with
regard to exposing, washing with warm water, drying, &c. The product
is a very thin sheet, having a mezzotint-like surface, with more or less
grain according to the action of the light. The white parts are perfectly
freed from the granular matter by the solution of the gelatine, while in
the darkest parts there is the greatest accumulation. The dry film in this
condition is pressed into soft metal, and by a double process of electrotyping
and subsequent facing with steel, a plate is obtained fit for printing
at the copper-plate press. The firm of Messrs. Goupil and Co., of Paris,
extensively employ this process for the preparation of the illustrations in
that elegant publication, “The Portfolio.” Another method of photographic
engraving lately projected by Mr. Woodbury is the following: a plate of
steel is covered with a layer of gelatine, mixed with a certain proportion of
gum and glucose, and dried in a dark room. This is exposed to the action
of light under a transparent photograph on glass. When afterwards this
gelatine layer is breathed upon, the moisture attaches itself to the portions
which have not been acted on by the light, and these become more
or less sticky. Sand or emery sifted to three different degrees of fineness
is then sprinkled over the plate, beginning with the coarsest, which
attaches itself to the most sticky parts. The less sticky parts are incapable
of retaining these larger particles; while the finest sand, which is sprinkled
on last, is held by parts of the plate that are even very slightly sticky; but
the places where the light has been intense are dry, and none of the sand
adheres. The gelatine layer is then completely dried, and the plate, being
covered with another of soft metal, is placed in a press, by which a granular
impression is produced on the soft metal, and this may then be copied in
copper by the electrotype process. The larger particles of sand produce
deeper depressions in the plate, and thus a gradation of tint is obtained.
Amongst other applications of the gelatine relief devised by Mr. Woodbury
is that of producing a watermark in paper. A very delicate relief is
firmly attached to a plate of steel or zinc, and when paper is rolled in contact
with these plates, it receives an impression of the design, all the delicate
half-tints being represented in the slight opacity of the paper. Mr.
Woodbury is at present engaged in perfecting a method for wedding his
own process to that of chromo-lithography, by first printing the different
tints on the paper, and then transferring the Woodbury prints to the top
of the colours. The transparency of the gelatine and ink is such that
the most brilliant effects are attainable in this way.
644Bichromated gelatine is also the agent employed in photolithography,
the image of a negative photograph being thus rendered insoluble in a
layer of gelatine spread on the stone, which is acted on by acids, &c., in
the usual way, after the soluble portions have been removed by water. As
there are also methods of using the lithographic process with plates of zinc
instead of stones, so there are processes of impressing the image photographically
upon the zinc. Of the general nature of the processes of
zincography, photolithography, and photozincography the reader will now
probably be able to form some idea, but the details need not here be
described. The last two, and some other processes for printing photographic
effects mechanically, all labour under the defect of imperfectly
rendering the half-tints of a picture. This remark does not apply to the
Woodbury process. The photo-lithographic process gives marvellous
results in cases where no gradations are required. Thus a whole page of
the Times newspaper may be lithographed in a space not exceeding half
of this page, and although the characters may be indistinguishable to the
naked eye, a lens will show them perfectly. Similarly, we may obtain
within the compass of an octavo page a photo-lithograph of one of
Hogarth’s large engravings, which will show every touch of the original
artist’s burin.
There is reason to hope that the time is not far distant when all our
tedious mechanical methods of reproducing drawings by wood or steel
engravings will be superseded by processes which will give us absolute
facsimiles of every touch of the artist’s pencil; and when some process,
giving all the delicacy and truthfulness of Mr. Woodbury’s prints, will
supply us with faithful transcripts of nature for book illustration at a cost
not exceeding that of the ordinary methods. So far as relates to one style
of drawing, these requirements appear to be nearly realized in the process
termed the graphotype, which reproduces mechanically, in the form of a
metal plate with all the lines in relief, a design which the artist has etched
on a flat surface. This is effected in the following manner: Chalk is
powdered very finely, and sifted through wire gauze having very narrow
meshes. A quantity of this is spread upon a smooth plate of metal, and
subjected to an intense pressure by means of an hydraulic press. The
particles of the chalk cohere into a mass, having sufficient firmness to
admit of its surface being drawn upon in the same manner as a block of
boxwood. The drawing is effected with an ink composed of lampblack and
glue, a finely-pointed camel’s-hair brush being employed; but the shades
must be produced by lines and strokes as in wood engraving. When the
ink is quite dry, the surface is rubbed with a fitch brush or with velvet;
and by this brushing the particles of chalk not protected by the inked
strokes are loosened and carried off. In a short time the chalk between
the strokes becomes quite hollowed out; and when a depth of about one-eighth
of an inch has been attained, every line remains standing in relief
exactly as in an engraved wood block. A strong solution of silicate of
potash is then poured upon the chalk, which its chemical action converts
into a kind of stone without in any way altering the forms. Although this
artificial stone is quite hard, so that impressions may at once be taken
from it, yet it is incapable of enduring the wear and tear of the printing-press.
Accordingly a mould is taken from it, and this is made, by some of
the processes of casting or electrotyping already described, to furnish a
metal stereotype plate.
645
Fig. 313a.—The Linotype Machine.
Among recent inventions in connection with printing, the linotype
machine calls for special mention. In this machine a great number
of actions are combined and co-ordinated with the utmost ingenuity,
but such mechanism does not lend itself to popular description, and we
must confine ourselves to a statement of what it effects, recommending
the reader to avail himself of some opportunity of seeing the apparatus
at work. It will not then be needful to give details of every
646one of the very numerous parts, which present in the ensemble a great appearance
of complication, the more so that much ingenuity has been
exerted to make the machine compact, which is a practical point of great
importance. The disposition of parts is not, therefore, that which is calculated
to show each movement clearly to the spectator, but that by which
the least space is occupied. The machine is driven by belting from a
main shaft, turned by a steam-engine, gas-engine, electro-motor, or other
regular source of power, and rotated at such a rate that the main pulley
of the machine itself (14½ inches in diameter) shall make about 60 revolutions
per minute. Fig. 313a shows the general aspect of the machine
and seat for the one operator required, but as we are not undertaking a
detailed and complete description of the whole mechanism, no letters of
reference are given; but the reader will be able, from the following
diagrams, to identify the more important parts, and form a general idea
of their action and purpose. In this machine great use is made of the
contrivances called cams, several of which may be observed in the sketch
towards the side of the machine on the left, being fixed on and turning
with its main shaft. They consist of plates, or open rims of various forms,
which move levers, etc., in any required way, and at any required period
of the revolution.
Fig. 313b.—A Matrix.
Fig. 313c.—Diagram of Movements.
Fig. 313d.—A Line of Matrices.
The linotype is not a type-setting and type-distributing machine, but
one in which the form is stereotyped line by line; hence its name of
linotype. The mould, or matrix, is made up of a number of brass matrices,
each of which consists of a flat plate having on its edge a letter incised.
One of these is represented on Fig. 313b wherein a is the hollow letter.
At the upper end the plate is cut into a number of notches like the
teeth of a saw, only that some of the teeth have their points cut off, leaving
steps, as it were, with faces parallel to the longer edges of the matrix.
There may be seen one of these at b, and on the opposite side of the V-shape,
three may be observed. The number and arrangement of the
cut-away notches is different for the matrix of each letter (or sign), and
special to it. The meaning of this will be seen presently. The diagram
Fig. 313c will help us to see how these matrices are assembled by touches
of the finger on the required letters as marked on the keyboard at D.
The matrices are assorted and stored in separate channels in the
“matrix” magazine, A, a portion of its cover being here represented as
broken off in order to show the channels. It will readily be understood
647that, by a system of levers connected with each key, the corresponding
matrix is released by means of an escapement (B´), and falls down one of
the channels E on to the travelling belt F, which conveys it to composing
648stick G, in which the matrices successively assemble in the order to
constitute a line (Fig. 313c), in which observe that the several words are
separated by spaces formed by long wedges of steel, the thick ends of
which hang down considerably below the line of matrices. These are
dropped one by one from a store at I (Fig. 313c), when required, by a touch
on the key-bar J; two of them are shown in position in the assembling
stick G. In Fig. 313a a bell is seen in front of the keyboard, and this is
automatically rung by a mechanical device when the line of matrices is
approaching in length to that allotted to the work. At this point the
operator has to consider whether he can complete the line with another,
or with how many syllables of a word, and he touches the keys of the required
letters. The assembling stick then contains all the matrices comparatively
loosely packed side by side, for the words are as yet separated
by only the thin edges of the space wedges. A touch of the operator on
a lever brings into play another part of the mechanism by which the composed
line is bodily lifted a short way, then moved horizontally, and
conveyed to the “mould wheel,” in which there is a slot, adjustable in
length and width, and the line is here firmly pressed against the face of
the wheel in such a way that the slot coincides with the line of hollow
letters on the edges of the matrices, as shown in Fig. 313b. This moulding
649arrangement is not the least ingenious device in this machine, and well
deserves attention. Before the moulding takes place, but while the line
is in its place, the wedge spaces are pushed up through the matrices by
another portion of the mechanism, and thus the line is immediately
“justified,” as the printers term it; that is, the wedges rise up, separating
the words, more or less, until the line has exactly its assigned length, and
the words are, at the same time, separated by equal spaces. A melting-pot
behind the mould-wheel contains a quantity of fusible metal, resembling
stereotype metal, which is maintained at just the temperature of
fluidity by a regulated gas burner. At the right moment a plunger is
forced into the fluid mass, causing it to rise through a kind of spout to
the level of the slot in the wheel, and be forced through that into the line
of letters. The metal instantly solidifies in the mould, the line of matrices
is removed on a bar to a new position at R, Fig. 313c, and the wheel then
makes a quarter of a turn, bringing the mould from the horizontal into a
vertical position (Fig. 313e). The linotype is subjected to the operation of
certain knives (not shown), by which it is pared smoothly to the exact thickness
and height required, and finally ejected, as shown in Fig. 313e, dropping
in its proper order into a receiving galley. The line, as completed, has the
shape represented in Fig. 313g, and a number of these lines assembled constitute
a “form,” answering all the purposes of the ordinary forms consisting
of separate type. These last, after having served their purpose, must be
“distributed,” that is, each single letter must be returned to the case from
which it was taken by the compositor; but the linotype form, after use,
is simply returned to the melting-pot for its metal to be recast into new
forms. The forms can, of course, remain standing for any length of time
at the mere expense of keeping the metal unemployed. One advantage
650of the linotype is that the printing is all done from new clean-faced forms,
instead of the old and dull-faced characters of ordinary type that have
been much used, but have to be resorted to under ordinary circumstances.
Fig. 313e.—A Finished Line entering Galley.
Fig. 313f.—The Melting Pot and Mould Wheel.
It may occur to the reader that errors in linotype would be much more
difficult of correction than those occurring with the ordinary type composed
by hand. If by chance a wrong matrix appears in the line, this
can be changed by hand at once; but supposing that the operator overlooks
some error in reading the assembled line, which, observe, he reads
with the characters arranged as they will appear in the impression, or
that he has misread his manuscript, and the line is cast, assembled into a
“form” with the rest, and then in the printed proof the error is discovered,
how is it to be rectified? Simply by removing the faulty linotype from
the form, and casting a new one. This is so quickly and easily done that
it has been found by actual test between linotype and ordinary type matter
containing the same defects, that the former could be corrected in less
than one-third of the time required for the latter.
We left the line of matrices at R (Fig. 313c), and we must now indicate
the method by which each is automatically returned to its own magazine,
an operation for which much ingenious mechanism has been contrived,
of which the details cannot be well described in this place. The line
651having reached R, the space wedges are disengaged from it and removed
to their receptacle at I, while the matrices become engaged by their teeth
in the grooves of a horizontal bar, and then the bar is grasped by a lever
which lifts it up to the distributing arrangement at the top of the machine,
where the teeth of the matrices come to the exact level of the grooves of
the distributor bar T. The line is then pushed laterally, the sides of the
matrices become engaged in the hollows of two parallel screws U, by
which, while suspended only by such of their inclined teeth as the corresponding
groove of the distributor can support, they are made to slowly
travel along from left to right until each reaches a certain point, namely,
that at which its sustaining V grooves on the bar are interrupted by cuts
which permit it to drop into its own special magazine. A little consideration
will show how, by various combinations of the notches on the matrix,
and corresponding cuts at the right places in the grooves of the bar, each
matrix may be made to move along until it reaches a determinate place,
and there dropped. Compare Fig. 313b and Fig. 313i. Each matrix thus
again deposited in its proper magazine has completed the circuit of the
machine, or, at least, has passed from the bottom of its magazine to the
assembling stick, hence to the mould, and, by the distributor, finds its
way back to the top of its magazine, whence, in its turn, it will descend to
perform again the same duty.
Fig. 313g.—The Finished Line.
Fig. 313h.—Lines assembled into a “Form.”
It must be understood that, beyond the operator’s touches on the key-board,
652and that required to send off the assembled line to the moulding
apparatus, all the actions are done automatically without the interference
of the operator, who, while one line is getting moulded, raised up, and
distributed, calmly proceeds with the composition of the following one.
Fig. 313i.—Matrices dropping into Magazine.
The rate at which the work is produced is very great. One good
operator with one machine can, it is said, turn out, hour by hour, matter
that would be equivalent to two and a half pages of this book, arranged
solid or without break. There are, of course, record performances of exceptional
operators who have completed more than twice as much as this
in a single hour.
653
Fig. 314.—Recording Anemometer.
RECORDING INSTRUMENTS. — THE PHONOGRAPH.
Sir John Herschel, in enumerating at the close of his inestimable
“Discourse on the Study of Natural Philosophy” the causes
of the rapid development of the physical sciences in modern times, assigns
a prominent place to the improvement of scientific apparatus, especially
of those instruments by which exact measurements or observations are
made. The accurate and elaborate instruments which serve for the delicate
and precise determinations and observations of modern science require
for their production a very advanced state of mechanical art, such as is
indicated by the perfection of the tools we described in a former article;
and these tools are themselves, on the other hand, the outcome of accurate
knowledge, and another proof of the interaction between science and
practical art. Since precise observations and accurate measurements form
the essential bases of every science, its progress will be accelerated by
every improvement in its instruments which increases their delicacy and
exactness. Indeed, hardly any branch of knowledge becomes entitled to
be called a science until it rests upon quantitative data of some kind.
Chemistry was nothing but a confused collection of vague notions until the
exact determinations of the balance were employed, and the proportions
of the substances combining or separating in chemical actions were found
to be related by certain simple and very definite laws. In all branches of
inquiry there is the same necessity of quantitative comparisons: lengths,
654angles, surfaces, volumes, masses, durations must be compared with standards
of their own kind; motions, forces, pressures, temperatures, lights
must be measured. The case of chemistry shows the line along which
other sciences are advancing. Physiology has made great strides since
instruments of precision have been used in its investigations, and as some
of these are of the kind we here propose to treat of, they will be described
in the sequel. To recording instruments, meteorology is also largely indebted
for the remarkable progress which it is making, and which will soon
place this branch of knowledge in a condition to supply the most striking
illustration of the difference between a science founded on accurate measurements
and a mass of vague observations.
The obvious advantage of a recording instrument (say, for example, such
a one as that represented in Fig. 314, which registers the force and direction
of the wind) is that the results are obtained without the immediate
attention of an observer, and they can be continuously recorded at every
instant, day and night; but there is another and yet greater advantage in
certain kinds of instruments which write their own records, in the fact
that they can be made to register results which would altogether escape
direct observation. It is said that a practised astronomical observer will
correctly record the time of a phenomenon to nearly the tenth of a second;
but there are cases in which we may desire to estimate time to the thousandth
part of a second or less. An investigation of M. Foucault has
already been named in which a far less interval of time was concerned
(page 387); but the recording instruments we have to mention here are
of use for enabling us to make certain instantaneous actions mark the time
of their occurrence with the greatest precision, and also for enabling us to
note the variations in actions which are too rapid to be directly observed
in their various phases.
Fig. 315 is a diagram which will serve to explain the method in which
the height of the barometer and the thermometer are registered in the
ingenious metereograph, invented by Professor Hough, of Dudley Observatory.
The contrivance has the advantage of performing the operation
for both instruments, with a single piece of mechanism and on the same
sheet of paper. The diagram is not intended to indicate the actual arrangement
of the parts of the apparatus, but merely to explain the principle of
its action. Let A represent a cylinder about 6 in. in diameter and 7 in.
high, covered with a sheet of paper, ruled with certain lines, some parallel
to the axis, and others perpendicular to those. This drum revolves by clockwork,
controlled by a pendulum, at a certain regular rate of, say, one turn
in seven days. B is a metallic bar or lever, about 2 ft. in length, mounted
on an axis or fulcrum at C. At D is a pencil or style projecting from the
extremity of the bar opposite the centre of the drum, but not in actual
contact with the paper. E and F are platinum wires attached to the lever
at about 3 in. distance from the fulcrum, C; E passes into the open tube of
a mercurial thermometer, G, and F into the shorter branch of a syphon
barometer, H. The clockwork has other offices to perform besides turning
the drum, A, on its axis; and one of these is to alternately elevate and depress
the lever, B, every half-hour. If the end, F, be depressed, it is plain
that the wire will come into contact with the metallic float, which is supported
by the mercury and follows its movements. If, therefore, wires from
a battery, K, including an electro-magnet, I, in their circuit, be connected
with the bar at C, and with the mercury at H, when the wire at F touches
the float, the current will pass and the armature of the electro-magnet will
655be attracted. The movement of the armature is so arranged that it causes
a blow to be given to the end of the bar D, so that the pen there marks a
dot on the drum, thus indicating its height at the time, and therefore that
of the mercury in H. When the lever is depressed at the other end, the
wire, E, similarly completes the circuit through the mercury in the thermometer,
and the height of the latter can be known from the dot which is
similarly impressed on the lower part of the paper. These movements may
be made with almost any degree of precision required. The clockwork is
also made to raise the hammers which strike the pen against the drum, at
the instant the electric current passes.
Fig. 315.—Registration of Height of Barometer and Thermometer.
The instrument, as actually constructed, registers also the height of a
wet-bulb thermometer, by another wire requiring a lower depression of the
lever to bring it into contact with the mercury in a wet-bulb thermometer.
A complete double motion of the lever requires one hour, and in that
interval the heights of the barometer and both thermometers are each
recorded once. The wet and dry-bulb thermometers are registered within
a minute of each other, and half an hour elapses between the barometer
and thermometer records.
Another invention of Professor Hough’s is a barometer which marks a
continuous pencil-line on a revolving cylinder, by which the variations of
the mercury are shown for every instant of the day. Another part of the
arrangement is a machine for automatically printing on paper in ordinary
characters the height of the mercury to the thousandth part of an inch.
656A very simple and trustworthy record of thermometric and barometric
heights is obtained by photography at Kew and elsewhere. A sheet of
sensitive paper passes horizontally at a uniform speed behind the tube of
the instrument, so that the only light it can receive must pass through the
glass. A lamp is placed in front, and a portion of the paper is protected
from its rays by the mercury, while those which pass through the tube
above the mercury make their impression on the paper, and thus record
the indications of the instrument.
Fig. 314 represents part of another ingenious meteorological instrument
invented by Mr. J. E. H. Gordon, and made by Mr. Apps. It is an
electrical anemometer, for indicating and registering the direction and
force of the wind. The apparatus consists of an external portion, which
is of course fixed on some high and exposed part of the building; and the
indicating and registering instrument, which communicates with the former
only by insulated wires connected with a galvanic battery, and which may
be placed on any convenient table within the house. The registering
apparatus in this instrument is very neat and compact, and the reader
will no doubt be able to form a sufficiently good idea of its nature from
the portion which is visible in the cut, and from the knowledge of similar
apparatus he may have derived from the descriptions already given in the
article on the electric telegraph.
Modes of making phenomena record the time and duration of their own
occurrence are now much used in all scientific investigations; and in connection
with the electric chronograph or chronoscope which we are about to
describe, few more efficient or elegant methods of “interrogating nature”—to
use Bacon’s phrase—have yet been devised. The reader who has
never seen an instrument of this kind will be the better able to understand
its principle by a simple illustration, which may very easily be made
a practical one by himself if he has a tuning-fork at hand. Let him fix
the tuning-fork firmly into a board in an upright position, by inserting the
part usually held in the hand into a hole in the board; and then attach to
the fork, by means of a little bees’-wax, a short bristle, which is to project
from the extremity of one prong in a direction perpendicular to the plane
in which the prongs vibrate. He has now only to provide himself with a
piece of glass a few inches square in order to obtain a record of the vibrations
of the fork when sounding. By the help of another piece of board
it will be easy to arrange a guide by which the piece of glass can be made
to fall down by its own weight in a plane parallel to the prongs, and in
such a manner that the free end of the bristle shall just touch its surface
during the whole time of its descent. Now let the surface of the glass be
blackened in the flame of a candle. If the glass be allowed to slide down
when the fork is not vibrating, the end of the bristle, by removing the
lampblack from the surface as the glass falls, would trace out a vertical
line. If, on the other hand, the blackened surface were itself not moved,
but simply brought into contact with the end of the bristle, while the fork
was sounding, there would be marked only a very short horizontal line,
corresponding with the extent of the vibratory movements of the prong.
When the glass is allowed to fall while the prong is in motion, the combination
of the horizontal movements of the bristle, and the vertical one of
the glass, will produce a waved line, which will exhibit perfectly regular
curves if the glass has been moved with uniform velocity. It is plain that
if the time taken by the glass to pass in front of the bristle were accurately
known, the number of movements per second executed by the prong of
657the fork could be found. On the other hand, if the rate of vibration of
the fork be known, the time occupied in the passage of the glass may
accurately be read off. If this simple experiment be understood, the
principle of the electric chronograph will be clear. Substitute for the
sliding glass a cylinder covered with white glazed paper which has been
coated with lampblack in the same manner; suppose the cylinder to
revolve at a uniform rate, while a tuning-fork is similarly writing its vibrations
on the surface of the paper, and let the same mechanism which turns
the cylinder, slowly draw the sounding-fork along a straight slide parallel to
the axis of the cylinder. The waved line will not form a complete circle on
the surface of the cylinder, but will be traced out in a spiral, owing to the
combined motions of the fork and the cylinder. As the number of movements
per second of a vibrating body emitting a given note are accurately
determined and perfectly regular, the waved line on the cylinder thus
furnishes an exact measure of small intervals of time, the utility of which
will presently be seen.
Fig. 316.—The Electric Chronograph.
Fig. 316 represents the apparatus as actually constructed. A is the
cylinder covered with the blackened paper, and driven by clockwork contained
in the case, B, the rate of movement being regulated by the conical
pendulum at C, so as to be approximately uniform. D is a lever for starting
and stopping the movement. The clockwork also causes the carriage,
E, to slide along the bars, F. This carriage bears three electro-magnets,
658and to the armature of each a fine pointed strip of metal is attached so as
just to touch the surface of the cylinder. The movement of the armatures
takes place in a direction parallel to the axis of the cylinder, and they are
acted on by independent currents, each electro-magnet having its own
binding-screws for the attachment of wires. The armature of one of these
is a steel bar, which vibrates in the manner of the prong of a tuning-fork,
at a rate known by the note it gives out. Sometimes, for delicate experiments,
the movements of this armature are checked and controlled by
introducing into its electric circuit a contact-breaker, formed of a real
tuning-fork, the vibrations of which are maintained by electro-magnets.
Another electro-magnet on the carriage, E, can be connected with the
pendulum of a standard clock, so that seconds may be also marked on the
cylinder, as larger units in the division of the time. In an electric chronograph,
which was exhibited at the International Exhibition of 1862, an
ingenious and excellent mode of making and breaking the electric contacts
from the standard pendulum was adopted. Two short vertical glass tubes,
placed side by side, had each near its lower end a small horizontal branch;
these branches were placed in a line with each other, with their ends in
very close proximity. The larger tubes were filled with mercury which
flowed into the horizontal branches, and the two streams joined in the
narrow space between the ends of the tubes. Although the mercury was
here unsupported by the glass, and surrounded by air only, it did not run
down, for the space was so small that the cohesion of the mercury itself
sufficed to keep the drop hanging between the two open ends of the tubes.
A very thin sheet of mica was carried by an arm of the pendulum, so
placed that at each complete oscillation the mica entered the space between
the two tubes and divided the mercury, and thus all electrical communication
between the two reservoirs was cut off. The mica remained during
one beat of the pendulum in this position; and at the commencement of
the return beat was withdrawn, allowing the divided columns of mercury
to flow together again, and complete the electric circuit. This admirable
make-and-break arrangement acted with the greatest regularity: the mercury
was not spilt, as might have been expected, there was no friction, and
any oxide formed by the spark which passed when the current was interrupted
was removed by the mica. The pendulum provided with such an
arrangement allows the current to pass, and interrupts it, during alternate
seconds, and the result is that the cylinder is marked with a regularly
divided broken line, thus, , the establishment and interruption
of the current at the end of each second being marked with great
sharpness and precision.
The third electro-magnet of the apparatus represented in Fig. 316 is
acted on by currents through the wires, G, H. The point attached to its
armature traces a plain spiral line on the revolving cylinder, except at the
instant when the current is established or interrupted. And the phenomenon
to be timed is in some way made to accomplish the making and
breaking of this circuit. This may be perhaps better understood by an
example. It has sometimes happened that the boxes employed in the
pneumatic dispatch stick fast in the tubes, and resist all efforts to dislodge
them by manœuvres with the compressed or rarefied air, or other means.
In such a case it becomes necessary to ascertain with tolerable accuracy
the position of the obstruction, so that the tube may be cut at the right
place and the obstacle removed. The known velocity of sound has been
ingeniously used for this purpose; the electric chronograph being made
659the means of ascertaining, to a small fraction of a second, the time required
for the report of a pistol to be propagated through the air of the tube and
reflected back from the obstruction. An elastic membrane is spread over
the open extremity of the pneumatic tube; this membrane has in the centre
a little disc of platinum, in electric connection with one of the wires, G, H.
The other wire passes to a galvanic cell or battery, and the return wire
from the battery is connected with a platinum point, the distance of which
from the disc can be adjusted with nicety by means of a screw, so that the
circuit may be complete only when the platinum point and the platinum
disc are in contact. The screw is adjusted so as to bring the point as
near as possible to the disc without actual contact. The chronograph
cylinder having been set in motion, a small pistol is fired into the pneumatic
tube through a side opening. Sound-waves of alternate compression
and rarefaction pass along the tube, and are reflected backwards and
forwards many times in succession between the obstacle and the membrane.
By these the membrane is alternately forced out and drawn in,
making and breaking the electric contact accordingly, and thus causing
the point of the electro-magnet to describe in the cylinder an indented
line, the intervals of which indicate the time the sound requires to traverse
the tube to the obstruction; and thus the position of the latter may be
known with sufficient accuracy.
A very interesting application of the electric chronograph is to the measurement
of the velocities of projectiles. The science of gunnery has
acquired an exactness unknown before electricity was made to carry messages
from the cannon-ball in its swiftest flight, and to write the record of
its own course. Instruments for thus measuring the velocities of projectiles
have been contrived by several electricians, among whom Wheatstone
appears to have been the first. The principle in most of these chronographs
is precisely the same as that on which the apparatus represented in
Fig. 316 is constructed. The action of the projectile which is electrically
indicated is the severing of a slender wire, which is stretched from side to
side of a wooden frame, so that it passes continuously backwards and forwards
in parallel lines. Thus a kind of screen is formed, through which
the missile must pass, and in its passage must rupture the wire. If the
wire conveys a current of electricity, this current is therefore interrupted
at the moment the ball passes. Sometimes the immediate effect of the
breaking of the wire is mechanical, as in Wheatstone’s arrangement, where
the wire is stretched by a weight over a series of pulleys, and attached to
a contact-maker, which completes the circuit when it is set free by the rupture
of the wire. A similar arrangement in the screens has been proposed
by Mr. Siemens for the establishment of circuits in connection with charged
Leyden jars, the sparks of the discharges being made to take place at the
surface of a revolving cylinder of polished steel, where the place is shown
by the spot they leave on the metal. M. Pouillet’s chronoscope dispenses
with the revolving cylinder, and measures the duration of the current established
by the projectile at one part of its course and cut off at another,
by the arc through which the needle of a galvanometer is impelled.
The instrument which has been most employed in this country by artillerists
is that invented by Professor Bashforth. Its indications are extremely
accurate, for readings may be taken to the two-thousandth part
of a second. From ten to fifteen screens are placed in the path of the
projectile at distances asunder which may vary from 15 ft. to 150 ft., but
which, of course, are carefully measured. Each screen is formed of a wire
660carrying an independent current, which also circulates in the coils of an
electro-magnet. The ten electro-magnets have styles attached to their
armatures in such a manner that when all the currents are passing, ten
parallel spiral lines are traced on the surface of a vertical revolving cylinder,
about 12 in. long and 4 in. diameter. The cylinder is covered with a sheet
of highly-glazed paper coated with lampblack; and when the sheet is removed,
the lampblack may be fixed on the paper if desired, and the record
made permanent. The equal intervals of time are marked on the same
cylinder by another electro-magnet connected with a pendulum beating
half-seconds. The axis of the revolving cylinder, &c., carries a heavy flywheel,
which is set in motion by the hand at the rate of about three revolutions
in two seconds, and the rest of the mechanism is thrown into
gear just before the signal to fire is given. The arrangement of the electric
connections at the screens is such that at the moment of the rupture
of the wire, the circuit is broken for an instant only. At this moment, the
iron of the corresponding electro-magnet ceasing to attract its armature,
the latter is drawn away by a spring; but the re-establishment of the current
immediately brings it back, and the style continues to trace the same
spiral line as before. The passage of the ball through the screen is therefore
marked by a little notch in the spiral line, thus, , and the
point where the deviation begins indicates the time at which the ball passed.
In order to read off this time, a straight-edge is applied to the cylinder
parallel to its axis; and by means of a scale sliding upon the straight-edge
the distances between the notches on the several spirals are compared
with those between the pendulum marks.
To record the instant at which a projectile passes determined points in
a cannon’s bore, lateral plugs are screwed in, each having, just projecting
into the bore, a small steel ball, which, pressed outwards by the passing projectile,
causes a cutter to divide the primary wire of a Ruhmkorff coil, whereupon
the spark that passes in the secondary circuit leaves its record on a
uniformly moving disc. Each plug has its own battery, coil, and disc.
A special feature of recording instruments may be exemplified by certain
applications of the principle to the investigation of physiological
actions. A skilled physician is often able to detect in the pulse of his
patient certain characteristics besides the mere rate, which are highly significant
as regards the condition of the circulatory system. The range of
these indications has been greatly extended by an instrument invented by
MM. Chauveau and Marey, by which the pulse is made to write down a
graphic representation of its action. The patient’s arm having been placed
on a suitable support, a little stud covered with soft leather is lightly pressed
against the artery by a spring. The stud is in contact with the shorter end
of a very light lever, the other extremity of which is furnished with a point,
which registers its movements on a cylinder of blackened metal, made
to rotate and advance longitudinally by clockwork; or the record is taken
on strips of flat smoked glass. As the motion is much magnified by
the lever, every variation in the pressure of the blood in the artery during
the beat of the pulse is distinctly and faithfully indicated. From the line
so traced the physician may obtain infallible data for judging of the condition
of the heart, the action of its valves, &c. It is marvellous to observe
the manner in which the curves of the sphygmograph, as the instrument
is termed, change their form when certain drugs are administered: the
change in some cases occurs immediately, so that the eye can detect by the
inspection of the sphygmographic curve almost the instant at which the
661drug was introduced into the system, and the nature
of its action on the heart.
Fig. 317.—Negretti’s Deep-Sea Thermometer.
Another instrument which is doing good service
in the hands of medical investigators is the spirograph,
in which the rise and fall of the chest in
breathing are similarly traced by the motions of a
lever. In this instrument a small pad, which presses
on the chest, communicates its movements to an
elastic membrane, which, like the skin of a drumhead,
covers one end of a cylindrical box maintained
in a fixed position relatively to the person of the
patient. The air in this box is in communication, by
means of a flexible tube, with the interior of another
similarly closed box; the elastic membrane of the
latter acts against the short end of a lever, which is
made to register its movements as in the sphygmograph,
for the compression of the air caused by the
rise of the chest is conveyed to the second box
through the flexible tube. The curves furnished by
this instrument also give valuable indications, and
exhibit marked changes under any influence in the
least degree affecting the respiratory system.
The value of a self-registering instrument for solving
problems, the intricacy of which is increased by
the multiplicity and rapidity of the actions to be
observed, cannot be better illustrated than by the
success with which Professor Marey has thus studied
some complicated actions of locomotion, as related
in his extremely interesting work entitled, “La
Machine Animale,” a translation of which has appeared
in “The International Series.” The action
of the horse in the various paces, walking, trotting,
galloping, &c., has been an endless subject of discussion,
with no other data than the shoe-marks left
in soft ground, and the general appearance of the
animal’s movements to an observer. But M. Marey—by
means of elastic bags containing air, communicating
the pressure through flexible tubes, so as to
move little levers, which write their traces on a revolving
cylinder impelled by clockwork, and carried
by the rider,—has completely and finally settled all
the points in dispute. It is now definitely known
how the horse’s feet are placed on the ground in each
of his paces, and the actual and relative time that
each foot remains down. The instruments are also
made to register the vertical movements of the
animal, so that a complete record of its motion can
be obtained.
Fig. 318.—Negretti’s Deep-Sea Thermometer, general arrangement.
It was long a difficulty to obtain data as to the
temperature of the sea at great depths below the surface.
It is obvious that the ordinary maximum and
minimum registering thermometers would not give
the temperature at any particular depth to which they might be submerged,
662but merely the temperature of the warmest or coldest stratum of water
through which they passed in their descent or ascent. No plan which has
been devised to obviate these difficulties appears to have been attended
with success, until a quite recent invention of Messrs. Negretti and Zambra
supplied the desideratum, and furnished a convenient instrument for trustworthy
determination of the temperature of
the ocean at any required depth. The same
firm long ago constructed thermometers for
deep-sea soundings, with bulbs protected
from the pressure of the water by an outer
covering of thick glass surrounding the delicate
bulb of the thermometer, between
which and the outer casing a space was left,
partially filled with mercury, so that heat
might readily pass to or from the inner bulb
without the latter being exposed to the
superincumbent pressure. The new recording
deep-sea thermometer differs, however,
from all other registering thermometers by
containing mercury only, without alcohol,
or springs, or other removable indices, and,
consequently, it is free from liability to derangement.
The following is the description
of the instrument:
In the first place it must be observed that
the bulb of the thermometer is protected so
as to resist the pressure of the ocean, which
varies according to depth, that of 3,000
fathoms being something like 3 tons pressure
on the square inch. The new instrument
is in shape like a syphon with parallel
legs, all in one piece, and having a continuous
communication, as shown in Fig.
317. The scale of the thermometer is
pivoted on a centre, and being attached in
a vertical position to a simple apparatus
(which will be presently described), is lowered
to any depth that may be desired. In
its descent the thermometer acts as an
ordinary instrument, the mercury rising or
falling according to the temperature of the
stratum through which it passes; but so
soon as the descent ceases, and a reverse
motion is given to the line, so as to pull the
thermometer towards the surface, the instrument
turns once on its centre, first bulb
uppermost, and afterwards bulb downwards.
This causes the mercury, which was in the
left-hand column, first to pass into the dilated
syphon-bend at the top, and thence
into the right-hand tube, where it remains, indicating on a graduated scale
the exact temperature at the time the thermometer was turned over. The cut
shows the position of the mercury after the instrument has been turned on
663its centre. A is the bulb; B the outer coating or protecting cylinder; C is the
space of rarefied air, which is reduced if the outer casing be compressed; D
is a small glass plug, as in Negretti and Zambra’s maximum thermometer,
which at the moment of turning cuts off the mercury in the tube from that
in the bulb, thereby ensuring that none but the former can be transferred
into the indicating column; E is an enlargement made in the bend, so as
to enable the mercury to pass quickly from one tube to another in revolving;
and F is the indicating tube, or thermometer proper. When the thermometer
is put in motion, as soon as the tube has acquired a slightly oblique
position, the mercury breaks off at the point D, runs into the curved and
enlarged portion, E, and eventually falls into the tube, F, as the instrument
resumes its original vertical position.
Fig. 319.—The Atmospheric Recording Instrument.
The contrivance for turning the thermometer over at the bottom of the
sea may be described as a vertical propeller, to which the instrument is
pivoted. So long as the instrument is descending the propeller is lifted
out of gear and revolves free; but as soon as the ascent commences, the
action is reversed, the propeller falls into gear with a pinion connected with
the thermometer, and by these means the thermometer is turned over, and
after one turn it remains locked and immovable. The engraving, Fig. 318,
shows the general arrangement, T being the thermometer, S a metal screw
connected with the frame of the thermometer by a wheel-and-pinion movement
at W; S† is the stop for arresting the movement of the thermometer
when it has made one complete turn.
664The atmospheric recording thermometer (Fig. 319) differs from the deep-sea
thermometer by not having the double or protected bulb, as it is not
required to resist pressures. In this form of the instrument, the thermometer
is turned over by a simple clock movement, which can be set to any
hour that may be desired. It is fixed on the clock, and when the hand
arrives at the hour determined upon, and to which the clock has been set
as an alarum clock is set, a spring is released, and the thermometer turns
over as before described. A wet and dry-bulb hygrometer is also arranged
on the same plan. For observatories, or where it is important to obtain
hourly or half-hourly records of the temperature, twelve or more thermometers
are placed on a frame, and these are turned over by clockwork one
after the other at every hour or half-hour as required.
The reader can hardly fail to perceive that powerful aid to the investigation
of the laws of nature must be afforded by such instruments as we have
described. And we have but taken an example here and there of the
scientific uses of the recording principle, selecting those that are most
readily understood, or that are connected with matters coming home to
the business and bosom of every one. The science of meteorology does
not deal with subjects which furnish merely amusing speculation for
the hour. Forecasts of storms and cyclones would often save many lives
and much valuable property; and our dependence upon meteorological
conditions cannot be more forcibly illustrated than by reference to the disastrous
floods which this year (1875) desolated some districts of France.
Meteorology has received a great impulse from the introduction of recording
instruments; and the vast number of results which are now hourly
recorded must lead to the certain development of the science, and its reduction
to exact laws. For even the winds obey laws—laws as definite as
those which control the motions of the planets; and could we but take
into account the whole of the circumstances upon which the movements
and other conditions of the atmosphere depend, we should be able to forecast
the weather with the same certainty as—thanks to the great and simple
law of gravitation—we predict eclipses or other astronomical phenomena.
Already, by aid of the telegraph, it is often possible to send a day’s warning
of approaching storms to localities lying in their probable track. The
Signal Service, which is a Department of the United States War Office,
has a corps of meteorological observers spread over the length and breadth
of the States, who send every eight hours, to a Central Office in Washington,
a report of the force and direction of the wind, height of the barometer,
&c. The officer at Washington sends back by telegraph to the public
press a synopsis of each day’s weather, and points out what weather will
probably follow; but if any city or port be threatened with a storm, special
telegrams are sent. Thus, a warning of the approach of a great storm,
which entered the American continent at San Francisco on the 22nd Feb.,
1871, was sent to Cheyenne, Omaha, and Chicago, twenty-four hours before
the storm reached these cities, which it was foreseen lay in its track.
Although the hurricane did much damage at some of these places, it
would probably have been far more destructive had not the inhabitants
been prepared for its approach.
An elegant form of barograph or recording barometer has been brought
out, which is small, but sufficiently accurate for all ordinary purposes. It is
founded on the aneroid, which, as everybody knows, is an instrument for
indicating atmospheric pressure by the changes of form it produces in a
thin circular metallic box, partially exhausted of air. The ordinary form
665of the aneroid is very sensitive and portable (sometimes it is made only
the size of a small watch), and bears an index needle moving over a
graduated disc; which arrangement is in the barograph aneroid, replaced
by a long lever, carrying an ink tracing point in contact with the face of a
cylinder that is caused by clockwork to make one revolution per week.
On the cylinder is spread a printed paper diagram, divided by lines for
each day of the week and each hour of the day, and on this the tracing
point marks a continuous curve, showing all the fluctuations of the
barometric pressure. The diagram is removed at the end of the week,
and a fresh form adjusted to the cylinder. The impressed papers thus
form a permanent and continuous record, from which the height of the
barometer, at any given moment, may be read off.
Everything yet contrived in the way of recording instruments is
eclipsed in wonder and interest by one which is among the latest
marvels of the age. It is a recording instrument, and more than a recording
instrument, for it can reproduce to the senses the very phenomena it
records; and these same phenomena are the most familiar in their effects,
and, at the same time, so subtle and delicate, that the impressions they
convey are not generally thought of otherwise than in connection with our
finest intellectual and emotional perceptions. We are alluding to the
phonograph, which can register for us music and song, and articulate
human speech in all their tones and modulations, and, like an aërial
spirit, address them to the ear again, as often as we wish, and thus
Inform the cell of hearing, dark and blind;
Intricate labyrinth, more dread for thought
To enter than oracular cave,
Strict passage through which sighs are brought,
And whispers for the heart, their slave;
And shrieks, that revel in abuse
Of shivering flesh; and warbled air,
Whose piercing sweetness can unloose
The chains of frenzy, or entice a smile
Into the ambush of despair;
Hosannas pealing down the long-drawn aisle,
And requiems answered by the pulse that beats
Devoutly, in life’s last retreats!
In order that the reader may understand the action of the phonograph,
it is necessary that he should know something of the science of sound.
Then we must remember that this word is commonly used to express
sometimes those sensations of which the ear is the organ, and at other
times the external cause of those sensations. It is with the former meaning
that we use such expressions as “a sweet sound”; with the latter,
such phrases as “sound travels.” It will not be necessary to speak of the
physiology of the organ of hearing; but attention should be directed to
the different kinds of audible perceptions we can distinguish, let us suppose,
when listening to a song: First, there is the pitch, or the notes in the
musical scale, which, by their particular sequence, constitute the air or
melody. Second, there is the degree of loudness or lowness of the notes.
Third, the enunciation, or those differences by which we distinguish, for
666example, the vowels a, e, i, o, u, one from another. Fourth, the quality of
the voice by which we can distinguish between two vocalists singing the
same vowel on the same note with equal loudness. Observe that these
four kinds of sound perceptions are independent one of another. The last
kind of difference may also be well illustrated by the instance of musical
instruments of different kinds sounding the same note, in which case the
difference of the quality or timbre is readily recognized. We have now to
show the nature of the mechanical movements outside of us which act on
the ear and reach our perception as sounds, giving the distinguishable
impressions that have been enumerated; and for the present we shall
consider the case of such musical sounds as those just referred to.
That the source of a sustained sound is an elastic body in a state of
vibration is a fact of which, in most cases, we are easily made aware
by the evidence of sight and touch; as a bell, a violoncello string, a pianoforte
wire, or a tuning-fork. On p. 656 is described a simple method by
which a tuning-fork may be made to write down its own vibrations, and
the more exact plan of recording them on the surface of blackened paper
on a revolving and advancing cylinder has also been referred to. By the
intervention of appropriate apparatus, a similar record may be obtained
from all sounding bodies. From observations of this kind, and others in
which totally different methods are used for counting the number of
vibrations per vibrations made in a given time, it is known that the pitch
of the sound or note depends on the rapidity of the vibrations—the
pitch rises with the number of them per second, and the relationship between
the notes of a musical scale depends entirely on these numbers.
Thus, when the vibrations for the eight notes of an octave are counted,
the numbers always have this proportion, beginning from the lowest note-–24,
27, 30, 32, 36, 40, 45, 48. Thus of the two notes—
as produced on musical instruments tuned to the concert pitch of the
present day, the lower corresponds with 264 complete vibrations per
second, the higher with 528. It will be observed, too, that all the
harmonies are determined by some simple ratio in the rates of vibration:
the interval of the fourth is 3, 4; that of the fifth is 2, 3, etc. Another
easily discoverable fact is that the loudness of the sound depends upon
the amplitude of the vibrations. This is sufficiently obvious by a few
experiments with a tuning fork; and by close examination of such tracings
as have been mentioned, we shall soon become aware of another circumstance—namely,
that the vibrations not simple, but that the larger or
general movement has one or more sets of small vibrations within it. In
Fig. 319a, A is the curve that would be traced by the tuning-fork in a state
of simple vibration; B and C are tracing such as are given by a fork in
two of its modes of vibration. The fork gives out its proper or fundamental
note in both cases; but the ear recognizes a difference in the
quality of the sound due to the smaller and more numerous vibrations.
Differences of the same kind are recognized in the notes produced by
different musical instruments; but these are usually more complicated,
and their forms are characteristic of the particular quality of the tone,
667which is thus shown to be due to the superposing of several related
systems of vibration upon the fundamental one. Thus three out of the
four qualities of sound recognized by the ear have had their physical
causes assigned. As for the fourth—namely, the distinction we perceive
among the different vowels sung on the same note—it has a physical
origin identical with the last. For since parts of the vocal organs assume
different positions in enunciating the different vowels, they constitute for
the time being so many varied musical instruments, and the graphical
traces of the sounds (for they can be obtained) show a corresponding
modification. Here, in Fig. 319b, for example, are represented the tracings
of the vibrations given to the air in various vowel sounds. It is also
through the vibrations conveyed by the air to the little membrane
called the drum of the ear that the sensations of sound are received,
and of the nature of these vibrations a few words must be said presently.
In considering the different qualities of sound, we have so far confined
ourselves to sustained musical notes, as, for instance, the vowel sounds in
singing. This has been done
to show the relations of rapidity
of vibration to pitch and for
simplicity of illustration of the
superposition of vibrations, etc.
Two other remarks must be
added—viz., that the vibrations
of musical tones are isochronous—that
is, whether the note be
loud or soft, the same time is
taken up in each vibration corresponding
with the same fundamental note. Other vocal
sounds than sustained vowel
notes are found to be due to
still more complicated combinations of vibrations of shorter duration,
and noises, as distinguished from musical sound, are formed also
by the superposition of a greater or less number of systems of
vibrations, the rapidities of which are wanting in harmonic relations
such as we have pointed out belong to the musical scale. Even in noises,
however, there is often one or more predominant systems of vibrations
668which a musical ear can detect. If the reader will hold a pencil or penholder
at one end and tap with it on the edge of the table, passing in
quick succession to parts progressively nearer where the pencil is held,
he will hardly fail to recognize a rising pitch in the little noises.
Fig. 319a.—Traces of Vibrations of a Tuning-Fork.
Fig. 319b.—Phonautographic Tracings of Different Vowel Sounds.
Fig. 319c.—Diagram.
Fig. 319d.—Phases of Sound Waves.
A word or two must be said as to the way in which sound is transmitted
through the air. This progression is commonly spoken of as a wave
motion, but it must not be thought of as taking place in the form familiar
to us as waves on water; still less must the reader confound it with the
sinuous lines shown in the graphical representations of vibrations given in
the figures. It is rather a series of rapid pulsations of the particles of the
air taking place in the direction in which the sound is propagated, and
resembling waves on water only by presenting periodical phases in uniform
succession. The difference may be illustrated from what may be seen in
a field of wheat when the wind is blowing over it. The stalks bend down,
and rise again when the breeze has passed, and thus the general appearance
of the waves of the sea is produced. If we confine our attention,
however, to the motion of the several ears of the wheat in a file of stalks,
we shall obtain a clearer notion of what takes place in the so-called waves
of sound. The positions of the stalks at some one instant of time may be
represented by the diagram, Fig. 319c. Each stalk is swinging backwards
and forwards like an inverted pendulum, and the successive phases of
these vibrations bring the adjacent ears nearest to each other about i,
and farthest apart at a and a´. The places of these, and
of all the intermediate degrees of approximation and
retreat, pass along the file. Instead of the ears of
wheat swinging on their elastic stalks, suppose particles
of air approaching and receding by virtue of the elasticity
by which they resist compression and recover from it,
and you will obtain an elementary idea of what takes
place in the transmission of sound. Fig. 319d is a
picture of a column of air acted upon by a tuning-fork. The swiftly
advancing prong is compressing the air in front of it, and in swinging
back it will tend to leave a vacuum behind it by which the air is partially
rarefied; and these alternate condensations and rarefactions will travel
669along through the air by virtue of its elasticity, and the mechanical action
by which they are able to agitate a stretched membrane (or other elastic
body), so that its vibrations will correspond with them in period and
magnitude, may be easily understood. The vibration produced is a simple
one, but any number of other systems may pass at the same time, and
each one will be propagated as if the rest did not exist, just as we may see
different systems of undulations moving on the surface of water. It
should be observed that the velocity of propagation is the same whatever
may be the period or the magnitude of the vibrations. The high and the
low, the loud and the soft notes of a piece of music played at a distance,
all take the same time in reaching the ear. Light as are the particles of air,
the mechanical actions which a number of them carrying strong vibratory
impulses will produce, may be illustrated by the rattling of window panes
by a loud peal of thunder, and may be bodily felt by a person standing
close to a very large bell while the hour is striking.
We have referred to instruments for registering sound, and even vocal
sounds, before anything has been said of the construction of the phonograph,
and it is, in fact, many years since the problem was solved of
recording the vibrations produced by speech. Mr. Leo Scott, in 1856,
invented an instrument, called the Phonautograph, which did this. It
consisted of a cone of sheet zinc like a large ear-trumpet, across the
smaller end of which was stretched a membrane, having attached to it a very
light style, which left a record of the vibrations of the membrane on a
blackened cylinder properly disposed to receive the tracing. When any
sound was produced near the open end of the cone, the impulses reflected
from its internal surface were concentrated on the membrane, throwing
it into corresponding vibrations. Now, this process could be reversed if
the tracing could be made to give back again to the style its original
movements, these transferred to the membrane would throw the air within
the cone into corresponding vibrations, and the sounds that gave rise to
the tracing would be reproduced. Yet Mr. Scott seems to have
suggested no such possibilities for his instrument; but a few years after
the invention of the phonautograph, M. Cros deposited at the Academy of
Sciences in Paris a sealed paper, which was opened after Mr. Edison had
patented the phonograph (1877), and found to contain suggestions of how
this might be done, but describing no experiments in which any approach
had been made towards realizing the conditions laid down. To Mr.
Edison belongs the honour of solving the problem by the invention of the
phonograph, which was patented by him in 1877. The device which he
happily hit upon for converting the phonautograph into a phonograph
was very simple in principle, and consisting merely in substituting a sheet
of tinfoil for the blackened paper in Scott’s apparatus, the mechanism
required for reproducing articulate human speech was thus found, contrary
to all expectations that had previously been entertained, to be essentially
of a remarkably simple character, for the arrangement of the parts was
even more direct than in the phonautograph itself. This is not derogatory
to the merit of the inventor, for every invention depends upon something
previously attained, and the discovery of suitable materials for the
various parts of the machine, and the many delicate adjustments of their
forms and disposition to secure the required object, demanded the application
of very remarkable experimental skill. The phonograph differs
from the phonautograph by giving up what it has registered in the
original form and material, and thus it is a speaking machine. It is a
670speaking machine which reproduces articulate speech, not produces it.
Much ingenuity has been devoted to the construction of speaking
machines which should be capable of producing the sounds of the human
voice. By throwing into vibration the air contained in cavities of certain
shapes, it was long ago found possible to produce sounds closely resembling
those of a voice singing particular vowels, and a real speaking
machine that could articulate words was exhibited in America before the
phonograph had been brought out. It was constructed by Mr. Faber,
and formed a very complicated arrangement, in which all the organs of
human speech were imitated. There were bellows acting like the lungs;
a larynx with various diaphragms, a mouth with movable tongue and lips,
and a tube to resemble the cavity of the nose. The positions and connections
of these parts were determined by levers acted from a key-board,
like that of a piano, and by certain pedals. By moving these in proper
order, the machine pronounced words distinctly enough, but in a strange
drawling tone. So like, however, were the sounds to those of the human
voice, that some accused the exhibitors of imposition, and unjustly
credited ventriloquism instead of mechanism with the results. It will be
observed that it is the function of the phonograph to reproduce, not produce,
human speech, and the mechanical arrangements of the instrument
are simplicity itself compared with Faber’s speaking machine.
Fig. 319e.—Edison’s Original Phonograph.
Fig. 319f.—Diagrammatic Section of Phonograph.
Fig. 319g.—The Graphophone.
Fig. 319e shows the form of the phonograph as designed by Mr. Edison
in 1877. It had a brass cylinder (A) upon which a narrow helical groove
was cut, and was mounted upon an axle (B), having a narrow screw-thread
corresponding with the groove on the cylinder, and working in the
upright (C), so that when the handle was turned the cylinder revolved,
and at the same time advanced in the direction of its axis. A heavy fly-wheel
(D) was attached, in order that the rate of motion might be nearly
uniform. A sheet of tinfoil, or of very thin copper, was wrapped round
the brass cylinder, and on this metallic foil rested the steel point attached
to the vibrating diaphragm, which was mounted in the ring (F).
This point was always adjusted so as to be over the helical groove in
the cylinder, and made to touch the tinfoil with a regulated pressure. E
671shows the manner of firmly supporting the diaphragm in such a manner
that it could be readily removed from the cylinder when the latter had to
be covered afresh with tinfoil, or the cylinder adjusted for reproducing
the sounds. The relation of the diaphragm and point to the tinfoil is
shown in Fig. 319f, which represents the apparatus in section. The tracing
point (t) is not attached directly to the vibrating diaphragm, but to an
adjustable spring (s), and interposed between the spring and the thin
metallic diaphragm is a little pad, formed of a ring of small india-rubber
tubing. When the mouthpiece (M) is spoken into, the sound vibrations
reach the diaphragm (g g) through the opening (o), and the movements
thus communicated to the point (t) which indents the tinfoil to various
depths, and with varying frequency, as the handle is turned, bringing
the whole length of the groove in succession to be operated upon. When
the instrument is required to reproduce the speech so easily recorded, all
that is necessary is to allow the indentations to re-act on the point that
made them. The cylinder is re-adjusted to the tracing point at the end
at which it began, the cylinder is set in motion, and the traces made on
the tinfoil move the point up and down, the vibrating disc (g) following
its movements, and thus communicating to the air a system of impulses
which are the counterparts in period, force and succession of those that
originally entered at o. It was usual to attach a conical mouthpiece to the
ring (F) in order to concentrate the reproduced sounds, which might then
be heard in all parts of a large room. When, in reproducing the sounds,
672the cylinder was turned with the same velocity as when the words were
spoken, the pitch of the voice issuing from the instrument was the same.
If it were turned quicker, the pitch was raised; if slower, lowered. The
words registered on the tinfoil could be reproduced two or three times,
but with decreasing distinctness, as the tracings gradually become obliterated.
However, the sheet could be removed from the cylinder, and the
speech reproduced at any place at any time afterwards by means of a
similar instrument, and a method of stereotyping was proposed for preserving
the records. The original phonograph was greatly improved
when well regulated clockwork was used for imparting motion instead of
the winch. Mr. Edison contrived a modification of the machine, which
made it much easier of manipulation, by substituting for the cylinder a
flat plate on which a spiral groove was cut. The plate was turned by
clockwork, while the vibrating point was made to follow the groove from
the centre to the circumference. The phonograph in its original form
reproduced speech with peculiarities of its own. The quality was metallic,
and reminded one of the intonation of the street Punch. It will easily be
understood that the disc itself must necessarily have its own systems of
vibration, and these will be further modified by the action of all the other
parts. Mr. Edison’s expectations of the capabilities of the instrument
673not being realized, he turned his attention, after several unsuccessful
attempts at its improvement, to the electric light and other subjects, at
the same time declaring his conviction that the perfection of the instrument
would be but a matter of time; in fact, within a very few years
afterwards such improvements were made on Mr. Edison’s instrument as
went far to justify this prophecy. These were the work of Dr. Chichester
Bell and Mr. Tainter, who, after long continued experiments, found in
paraffin wax, with a small admixture of some other substances, a better
material for receiving the impressions. A cutting style made to act upon
this cuts out a fine groove, the bottom of which is not a series of indentations,
but a continuous wavy curve, representing every degree of inflection
the vibrating diaphragm. In the new form of the instrument, Fig. 319g, which
was called the graphophone, to distinguish it from Edison’s, the cylinder
does not move forward: it is the diaphragm that advances parallel to the
revolving axle. The cylinder is driven by a treadle, like a sewing-machine,
and there is an ingenious arrangement by which the speed is
controlled so that it can be maintained quite uniform. The movement
of cylinder and style can be instantly arrested by touching a button, and
as readily re-started. Quite recently Mr. Edison has returned to improving
the phonograph by using rather thick, solid cylinders of wax, which
are previously prepared for use by the instrument itself paring them down
to a truly cylindrical and perfectly uniform surface, the result being a
great increase of clearness in the speech and tones of music. Mr. Edison’s
new instruments are driven by small electro-motors, and the speed is regulated
by a centrifugal governor. It is said that these wax cylinders are
capable of giving out the same record for a thousand times without perceptible
sign of deterioration; and when the cylinders are required to
receive a fresh impression, a former one can easily be pared off. The
machines can be arranged so as to sound loud enough to be heard by a
large assembly; but the quality of the tones of speech or music is most
perfect when conveyed from the receiving chamber in front of the
diaphragm to one or both of the auditor’s ears by means of a short elastic
tube. Half a dozen persons can thus hear the record on the cylinder
with such marvellous distinctness as to be able to recognize the tones of a
known voice. The very latest form of the instrument, as it has just left
Mr. Edison’s hands, is represented in Fig. 319h. In this one single very
small diaphragm serves both for recording and reproducing the sounds.
This is made of extremely thin glass, to which is attached a small projection
made of celluloid, which acts on a bar that carries the recording
point. The configuration of this point is most ingenious and peculiar, for
it is, in fact, double, one part being shaped like a gouge, which cuts into
the walls of the minute depression traced on the wax cylinder, while a style-shaped
part impresses the wax with punctured indentations. The shaping
of its forms is a difficult and delicate operation, for they are very small and
are cut in sapphire. The reproduced speech given out by this instrument
is said to possess the properties of sharpness and clearness in a remarkable
degree. The machine is provided also with a sapphire cutting edge,
by which an old record may be pared off by the very motion of the cylinder
in receiving a new one. This phonograph is put in movement by ingenious
mechanical devices, for giving uniform rotation from such motive
power as may be supplied by the foot or by water or by clockwork. This
improved instrument lays claim to practical utility, and its manufacture
will, it is stated, be shortly commenced on a large scale.
674Quite recently there has been established in America a big manufactory
of phonographs in the form of a toy, which is sure to become very popular
everywhere. Here they turn out daily several hundred real speaking dolls,
which contain clockwork actuating a phonographic cylinder impressed
with the words of some childish story or simple rhyme, such as “Jack and
Jill,” “Mary Had a Little Lamb,” etc. Each doll of course repeats its little
tale as often as the clockwork is set going. These toys are adapted to all
nationalities; for, besides many English, there are a number of French,
German, Italian, etc., girls employed doing nothing all day long but addressing
appropriate words to each little automaton’s waxen cylinder.
Fig. 319h.—Edison’s Perfected Phonograph.
The capabilities of the phonograph suggest some curious applications
that may be made of it. For example, the songs of a fine singer may
thus, in all their modulations, reach people in distant lands, or be made
audible to future generations. Thousands of people in England have
heard with their ears, through Mr. Edison’s instruments lately brought
over by Col. Gournaud, songs and speeches, and pieces of concerted
music, sung, said, or played in America months before. Music can be
bottled up, so to speak, without the consent of the originators; and,
indeed, it is said that an eminent prima donna has applied for an injunction
to restrain certain phonographers from reproducing her vocal
triumphs with their instruments. A speech of Mr. Gladstone’s, delivered
in England, has been phonographically heard in New York with great
applause. There is no reason but what, with a loud speaking phonograph
uttering an orator’s very words and tones, while instantaneous photographs
of his successive gestures and attitudes are projected on a screen,
a true and lively impression of his eloquence might be conveyed centuries
after his decease. One is almost led to speculate as to the consequences
if these nineteenth century inventions had been antedated by a few
thousand years: what stores of knowledge we might now possess! and
how pleasant it would be thus
To hear each voice we feared to hear no more!
Behold each mighty shade revealed to sight,
The Bactrian, Samian sage, and all who taught the right!
675
Fig. 320.—The Domestic Aquarium.
AQUARIA. — THE CRYSTAL PALACE AQUARIUM. — THE BRIGHTON AQUARIUM.
Under the date of May 28th, 1665, the curious gossiping diary of
Samuel Pepys contains this entry: “Thence to see my Lady Pen,
where my wife and I were shown a fine rarity; of fishes kept in a glass of
water, that will live so for ever—and finely marked they are, being foreign.”
This doubtless refers to the now well-known gold fishes, which about the
time alluded to were introduced into Europe from China, where they had
probably been for ages reared and kept in captivity, chiefly for the sake of
ornament. Perhaps the reader may be disposed to think that, therefore,
the aquarium cannot be distinctively a nineteenth century invention, nor
at all a modern invention, in principle at least; but merely the “glass of
water,” or the globe of gold fish on a larger scale. Such a notion would be
quite incorrect, for the principles which are embodied in the modern
aquarium were not recognized and applied until quite recently. Aquatic
animals kept for a period in vessels in which the water is changed from
time to time cannot be considered as properly forming an aquarium. The
beauty and value of a well-regulated aquarium depend not merely on the
opportunities it affords of studying the habits of the animals; the spectacle
it presents has a far wider interest, as illustrating and confirming the conclusions
of science regarding certain great principles which govern the
whole animal and vegetable life of this terraqueous globe. Perhaps in the
whole range of nature nothing is more wonderful than the direct interdependence
of animal and vegetable life, and the exact balance between
them, which preserves the composition of the atmosphere unchanged. The
constituents of the atmosphere have an immediate relation to both forms
676of life. No animal can live without a supply of oxygen gas, which it absorbs
and replaces by carbonic acid gas. The latter, on the other hand, is absorbed
by plants, for these, under the influence of light, decompose the
carbonic acid, returning the oxygen to the atmosphere, thus purifying the
air by again fitting it for the respiration of animals.
It might be supposed that animals which live entirely beneath the surface
of water are removed from the influence of atmospheric oxygen, and
that they form exceptions to this law. But such is not the case, for water
absorbs and holds in solution a certain quantity of air, the oxygen of which
is taken up by aquatic animals. In the lower forms of animals inhabiting
water, the absorption of this vital element takes place at the general surface
of the body; but in the more highly organized creatures there are
special organs appropriated to this purpose, of which the gills of a fish
may be cited as a typical example. The giving out of carbonic acid is an
action as universal in the animal world as the absorption of oxygen, and
all aquatic animals tend to charge the water in which they live with this
gas. Fish, or any other water animals, will soon die if they are placed in
water from which all the air has previously been expelled by boiling, or by
placing under the receiver of an air-pump. In this case the creature dies
from want of oxygen; but it would also die, even if supplied with oxygen,
were the poisonous carbonic acid emitted by itself allowed to accumulate
in the liquid. In nature, this carbonic acid forms the food of aquatic plants
and sea-weeds, and these restore oxygen to the water. If a bunch of watercresses
be placed in a bottle filled with water, and exposed to strong sunshine,
the leaves may soon be seen covered with small bubbles of gas.
This gas may be collected and examined by a suitable arrangement of the
bottle, and it will be found to be pure oxygen.
The merit of having first imitated the plan of nature for the preservation
of aquatic animals appears to belong to Mr. Ward, the inventor of the
“Wardian cases” for ferns and other plants. He, in 1841, formed in
London a fresh-water aquarium, in which, for the first time, the animals
were kept in a healthy condition by the compensating action of plants.
Mr. Gosse, Dr. Price, and others, made experiments with marine animals
and plants, about 1850. Mr. Mitchell, who was then secretary to the
Zoological Society of London, saw about this time a small aquarium on
the balancing principle at Dr. Bowerbank’s, and this suggested the erection
of the fish-house in the Zoological Gardens, Regent’s Park. This was
opened in 1853, being the first public aquarium ever constructed. The
tanks remain at the present time in nearly their original condition, and
this aquarium has been remarkable, not only as predecessor of the many
public aquaria which have since been erected, but for having given rise to
a movement in favour of aquaria as domestic establishments. The setting-up
of household aquaria became almost the rage of the day, and so many
books and magazine articles devoted to the subject appeared during the
ten years following the establishment of the Regent’s Park aquarium, that
the literature of the subject is quite considerable. Mr. Gosse showed how
water for marine aquaria could be produced by adding to fresh water the
solid constituents of sea-water; and, in the marine aquaria of some inland
towns far distant from the sea, this artificial sea-water is the only kind
used. After the establishment of the Regent’s Park aquarium, public
aquaria were opened successively in Dublin, Galway, Edinburgh, Scarborough,
Weymouth, the Crystal Palace, Brighton, Manchester, and Southport;
and on the continent at Paris, Hamburg, Hanover, Boulogne, Havre,
677Brussels, Cologne, Vienna, and Naples; also in North America at San
Francisco, and in other places. The general interest in public aquaria,
and especially marine aquaria on the large scale, seemed to increase as
the comparative failure of the domestic tanks lessened the taste for them.
The causes of the failure so often attending the attempt to maintain aquaria
on the small scale arise partly from the amateur naturalist’s want of
exact knowledge, and the great amount of attention and care required, and
partly from the inherent difficulties of the subject. An aquarium, even on
the largest scale, and with every appliance that science can suggest, only
represents, after all, a few of the conditions which actually exist in nature;
but in small vessels, with a limited quantity of water, without the continual
motion of the liquid, which belongs naturally to seas and streams, and
with circumstances of light and temperature widely different from those
which are obtained in nature, it is not surprising that the success of domestic
aquaria should be but very partial, and that the taste for them
should have declined accordingly.
Many public aquaria proved commercial failures; but we select for
special description two which have been thoroughly efficient, and are remarkable
for size, reputation, and successful management. The arrangements
at these two institutions as regards the aëration and renewal of the
water are, however, quite different. Some plan by which the same sea-water
might be supplied with oxygen, and kept in a clear and pure condition,
was necessary for the very existence of the inland marine aquarium
at the Crystal Palace, whereas the position of Brighton made the natural
sea-water more available. The success of the former method at the Crystal
Palace Aquarium, under the judicious system adopted by Mr. W. A. Lloyd,
the superintendent, perhaps renders this aquarium one of the most interesting,
in a scientific point of view, of any yet in operation. The water
here is never changed by the addition of sea-water; but fresh water is
added as required, simply to supply the loss by evaporation; and any solid
constituents which the animals may abstract from the water as material for
their shells is replaced, so that the ordinary composition of sea-water is
maintained. This is merely imitating Nature, for the evaporation from
the surface of the sea is compensated by the fall of rain and the influx of
rivers, the latter constantly bringing in the various salts held in solution.
The following particulars regarding the Crystal Palace Aquarium are derived
from Mr. Lloyd’s excellent handbook, which contains not only clear
descriptions of the inhabitants of the tanks, but interesting historical
notices and a well-written disquisition on the principles which should
regulate the construction and management of aquaria.
The building was commenced in July, 1870, and was opened in August,
1871. It was designed by Mr. Driver, of Victoria Street, and presents
an admirable simplicity, which entirely accords with the purpose for which
it was erected. The whole available space has been occupied, and nothing
has been wasted on unmeaning or fantastic embellishments. Even the
decorative shams, in which ordinary painters delight, have been excluded.
No part of the walls or of the woodwork is painted to look like marble, or
678even to imitate oak. The building, which is about 400 ft. long and 70 ft.
broad, is situated at the north end of the Palace, partially occupying the
site of the portion which was so unfortunately burnt down in 1866. It is
but one storey high, and besides a large reservoir beneath the floor, holding
100,000 gallons of sea-water, there is a series of sixty tanks, with thick
plate-glass fronts, which collectively contain 20,000 gallons of water. This
water, weighing over 1,000,000 lbs., was brought from the coast and conveyed
to the Palace by the Brighton Railway Company at a very moderate
rate. For many weeks after the water was placed in the reservoir and tanks
it was very turbid, from taking up the lime used in their construction and in
that of the rockwork. In this condition it was very alkaline; but the lime
was slowly precipitated by the carbonic acid of the air, the water became
clear, and vegetation appeared in the tanks. The great capacity of the
reservoir facilitates the cleansing of the water; for, supposing that the water
in one of the tanks, holding, say, 6,000 gallons, became turbid from any
cause, the water from this tank could be run off into the reservoir, where its
mixture with the much larger quantity would not sensibly affect the purity
of the mass, from which within half an hour the tank could again be filled.
All the tanks are constantly receiving water from the clear and cool
reservoir below, in which there are no animals, so that the motion of the
water in the tanks, like that of the ocean, is incessant. The water issues
from the pump at a rate (indicated by a counter) of from 5,000 to 7,000
gallons per hour. The pump is worked by a steam engine of three horse-power,
and the machinery requires the unremitting attention of three
engineers, who succeed each other by turns, each working for eight hours.
Two sets of the machinery—pumps, steam engines, and boilers—are provided,
one being always kept in reserve, ready for use in case of any accident.
Even in winter, when, from the lower temperature, the water contains
the largest amount of oxygen, it is found that the stopping of the circulation
of the water for only a few hours occasions manifest discomfort to
some of the animals. The water is poured into the two centre tanks in
an equally divided stream, and by a simple fall of a few inches from tank
to tank it flows by two routes to the lowest tank, from which it passes into
the reservoir below. This incessant circulation of the water constantly
exposes fresh surfaces to the action of the air, by which oxygen is absorbed.
But besides this, other small streams of water are made to forcibly enter
the tanks from jets, by which a large quantity of air is carried down in very
small bubbles. The removal of carbonic acid is accomplished by the
vegetation which spontaneously makes its appearance in sea-water under
suitable circumstances. It has been found quite unnecessary to introduce
purposely any kind of sea-weeds, for the spores of low forms of vegetation
are always present in the water, and they develop rapidly under the stimulus
of light. Indeed, one of the difficulties of aquarium management is to
avoid this excessive vegetation by limiting the light as much as possible,
and yet leave sufficient illumination for the observation of the animals. The
amount of light falling upon each tank is very carefully attended to at the
Crystal Palace, and where it cannot be diminished sufficiently to check the
overgrowth of vegetation, without at the same time interfering with a proper
view of the animals, certain molluscs and fishes which live upon algæ are
put into the tanks to consume them. This spontaneous vegetation is so
vigorous that a comparatively small quantity suffices to remove from the
water all the carbonic acid which it may derive from the animals and
decomposing matters.
679It should be mentioned that at this aquarium the water is never filtered,
but its clearness is obtained merely by the perfect system of circulation. The
unused food and excrementitious matters are oxygenated by the air which
the water abundantly holds in solution—thanks to the surface exposed in
its constant circulation, the injection of the jets of water carrying minute
bubbles of air into the mass of water, and the gas given off by the vegetation.
The whole process of purification is therefore chemical, and the success
and excellent adaptation of the system may be judged from the fact
that the water seen in masses 9 ft. deep appears perfectly clear and bright.
The building is very cool in summer: even in extremely hot weather the
temperature of the air within it is never higher than 68° F., and that of
the water in the tanks never exceeds 63°. In winter the temperature of
the air is maintained by hot-water pipes at from 60° to 65°, and the temperature
of the water at about 55°. On winter evenings the aquarium is
illuminated with gas, and the habits of many nocturnal animals can then be
conveniently studied.
Fig. 321.—The Opelet (Anthea cereus).
“All the animals in this aquarium,” says Mr. Lloyd, “have to be fed
constantly; and as for the sea-anemones—of which there are in the aquarium
over 5,000 individuals—every one of them has a morsel of food proportioned
to its size, and according to the condition of the water, given it
at frequent intervals with a pair of wooden forceps by an attendant who
makes this his sole occupation—as these flower-like creatures, being so
non-locomotive as to be almost absolutely fixed, cannot pursue their food,
or in an aquarium obtain it in any other manner. They are here deprived
of the action of the waves, which in the actual ocean brings them nutriment,
which is arrested by their outspread and waving tentacles. The
food consumed by a few of the animals now present in the aquarium is
680vegetable, consisting of green weeds (Ulva, Porphyra, Enteromorpha, &c.),
but by far the greater number have animal food given them. This consists
of shrimps, alive or dead, crabs, mussels, oysters, and fish, but they are
never fed on butcher’s meat.”
The creatures known as “sea-anemones” are well represented in the
Crystal Palace Aquarium. The observer cannot fail to be struck by their
resemblance to flowers, from the radiated arrangement of their tentacles,
and the beautiful colours they often exhibit. The opelet (Anthea cereus),
Fig. 321, is perhaps the most beautiful among British species, and is a
conspicuous denizen of the Aquarium, where its long green tentacles, tipped
with lilac, are commonly seen expanded or twisting about like so many
snakes. These tentacles are stretched out in search of food, and when by
chance an unlucky shrimp or other suitable prey merely touches a tentacle,
it is seized and held with remarkable pertinacity, the rest of the tentacles
closing round it. The mouth of the creature, placed in the centre of the
disc, then expands to an extraordinary size, and the prey is quickly lodged
in the capacious digestive sac of the actinia, where the soft parts are soon
dissolved, and the hard indigestible residue is ejected by the mouth. The
tentacles of Anthea, and of other species belonging to the same subdivision
of the animal kingdom, are furnished with an immense multitude of curious
organs, which consist of cells or minute bags, containing coiled up within
them a slender highly elastic filament. When these cells are compressed,
the filament shoots out of its capsule to a surprising length; and it has
been supposed that the adhesive power of the tentacles depends upon
these filiferous capsules; while it is not improbable that some virulent
fluid is also emitted from the cells, for the victims appear as if paralysed
almost as soon as they are seized. Our knowledge of these animals has
been largely extended by the opportunities of observing their habits which
are afforded by marine aquaria.
To obtain the variety of animals requisite for stocking a public aquarium
is by no means an easy matter; for the animals must be good specimens,
in a healthy condition, uninjured by their capture or transport from the
sea. The Crystal Palace Aquarium Company have at Plymouth a large
pond, which communicates with the sea at every tide; and this, under the
superintendence of the company’s resident agent, serves as a store for
animals. Similar arrangements exist at Southend, Weymouth, Tenby, and
other places. The specimens are brought to Sydenham by fast trains—special
facilities being afforded by the railway companies for this purpose.
The mode of carrying the animals depends upon their nature, and is sometimes
a matter of no little difficulty. All fishes, except perhaps eels and
blennies, must be carried in a sufficient bulk of water; and then the due
681oxygenation of the water and the removal of the carbonic acid can be but
very imperfectly accomplished. A considerable mass of water is absolutely
necessary in such cases, and the difficulties and cost of the transit are
much increased by its weight. In warm weather the quantity of oxygen
retained in the water is materially diminished, and under such circumstances
the creatures would soon perish. On the other hand, in very cold
weather the temperature may be so far reduced below that suited to their
habits that death may also result from this cause. Crabs, lobsters, sea-anemones,
sea-urchins, and similar animals can in general be carried without
being immersed in a mass of water. These animals are placed in
layers of wet sea-weed contained in baskets, so that the air has access to
the moisture which covers the bodies of the animals, which is prevented
from drying up by the humidity. As in this case the small quantity of
water exposes a very large surface to the air, oxygen is plentifully supplied.
Mr. Lloyd points out that it is owing to the readiness with which mere
films of water are aërated, that it has been found possible to convey to
Australia the eggs of salmon and trout, and hatch them there. They could
not have been carried in water, but they were successfully conveyed when
surrounded by a cool and very moist atmosphere. This mode of transmission
is much more economical and convenient than the plan of carrying
the creatures in water, and it is therefore resorted to whenever the organization
of the animal permits.
Fig. 323.—The Lancelet (Amphioxus lanceolatus).
Specimens of a very remarkable creature are, or lately were, exhibited
at this aquarium in the lancelet (Amphioxus lanceolatus), Fig. 323, which
animal itself is a comparatively recent discovery. It is about 2½ in. long,
and although it is fish-like in form, it presents so many points of structure
common to lower animals, that it is looked upon by naturalists as a link
682between the molluscs and the fishes—being the lowest of the latter in
organization. The creature can hardly be said to possess a skeleton, the
tissues representing that structure are so soft. It has no definite brain,
but it possesses olfactory and optic organs of a rudimentary kind.
The Brighton Aquarium, already so well known as a place of popular
resort, is a structure of considerable architectural pretensions, and is
the largest establishment of the kind in existence. The idea of this undertaking
appears to have originated with Mr. E. Birch, the engineer of the
actual structure, who, having, in 1866, visited the aquarium at Boulogne,
perceived that the construction at Brighton of a marine aquarium on a very
extended scale offered every promise of commercial success. The promoters,
in 1868, obtained from Parliament an act authorizing them to acquire a
certain site for the aquarium, but imposing such limits as to the height of
the structure that it was necessary to place the greater part of the building
below the level of the ground, a matter involving considerable engineering
difficulties. The aquarium is situated close to the Chain Pier and immediately
below the cliff, the building being protected from the waves by a
strong sea-wall of concrete and Portland stone. The building was definitely
opened in August, 1873, while the meeting of the British Association
was being held in the town. Its length is no less than 715 ft., and its
average width 100 ft. The predominant element in the architectural style
of the building is Italian. The following particulars as to the arrangement
and dimensions of the various parts of the building are derived from the
official guide-book:
Entering the gates at the western end, the visitor finds himself at the
top of a flight of granite steps leading to the entrance court, 60 ft. by
40 ft. The front elevation of the building is 18 ft. high, and consists of
five arches, with terra-cotta columns and enrichments. On the frieze
running round the sides are the appropriate words, “And God said, Let
the waters bring forth abundantly the moving creature that hath life.” On
the northern side of the entrance court is the restaurant; and on the
southern side a series of niches ornamented with vases. From this outer
court, the entrance hall, which is 80 ft. by 45 ft., is approached through
three doors. This is furnished with reading-tables and supplied regularly
with periodicals, journals, and telegrams; while between the pillars supporting
the roof are handsome pedestals, surmounted with large glass
vases containing the smaller interesting marine and fresh-water animals,
which would be lost to view in the larger tanks. In one of the recesses
facing the entrance are four microscopes, in which specimens illustrative
of subjects in natural history connected with the aquarium are constantly
exhibited. To the north of the hall lie the general manager’s offices, the
retiring-rooms, kitchen, &c.; and eastwards, in a direct line with the restaurant,
is the entrance to the western corridor of the aquarium proper.
This corridor, which contains a great many tanks, is the longest of
any: it extends 220 ft., and is broken by a central vestibule, 55 ft. by
45 ft. The roof, which is groined, is constructed of variegated bricks,
683and rests upon columns of Bath stone, polished serpentine marble, and
Aberdeen granite, the carved capitals of the columns having appropriate
marine subjects. On each side are placed the first two series of tanks,
twenty-one in number. These increase in dimensions from 11 ft. by 10 ft.
upwards, the largest measuring over 100 ft. in length by 40 ft. in width, and
holding 110,000 gallons of sea-water. This colossal tank is the largest in
the building, and is devoted to the exhibition of porpoises, turtles, and
other animals of large size. The next largest tank, 50 ft. by 30 ft., is immediately
opposite.
Fig. 324.—Sea-Horses (Hippocampus brevirostris).
The eastern end of the western corridor opens upon the conservatory,
which serves as an approach to the rockwork, fernery, and picturesque
cascade, and also to the eastern corridor. Some artificial rockwork, skirting
the north side of the conservatory, is traversed by a stream of water,
broken up at intervals so as to form numerous little bays and ponds, and
utilized for the reception of seals and the larger reptilia. In the side-space between
the conservatory and the second or eastern corridor are six octagonal
table-tanks, of elegant design, for the exhibition of some of the smaller and
more rare marine animals, and, at the eastern extremity, apparatus which
serves to illustrate the hatching and development of trout and salmon. The
entire length of this second corridor is about 160 ft., one side of the eastern
portion, which is 90 ft. by 23 ft., being devoted to the exhibition of fresh-water
animals. At the end of the corridor are situated the curator’s offices
and the naturalists’ room, fitted with open tanks and all necessary appliances;
and the engines, pumps, &c., for supplying the water, and keeping
it constantly aërated.
The system adopted for aërating the water at the Brighton Aquarium is
quite different from that used at the Crystal Palace. In the former the
water is pumped directly from the sea into reservoirs formed under the
floors, and capable of holding 500,000 gallons, which can be filled in ten
hours. From these the water is pumped up into the tanks as required; but
there is no general circulation through the system of tanks and reservoirs.
684Each tank is treated independently, and its water is aërated and kept
moving by the injection of air at the lower part, effected by steam power.
The popularity of the Brighton Aquarium may be judged of from the
fact that the average daily
number of visitors is about
9,000, and that on some occasions
nearly twice that
number pass the turnstiles.
Among the specialities of
the establishment are herring
and mackerel, which it has
hitherto been considered impossible
to preserve in confinement
for any length of
time. They are now thriving
well in the Aquarium, although
these fishes are both
extremely impatient of confinement.
The herring feed
readily upon small shrimps, in
catching which they display a
wonderful activity. Fig. 324
shows the curious fish called
the “sea-horse” (Hippocampus),
from the singular resemblance
of the front part of the
body to a horse’s head, or, at
least, to that form which
conventionally represents the
“knight” among a set of
chessmen. The tail of the
creature is prehensile, and
enables it to cling to sea-weeds
and other bodies. The sea-horses
have thriven well in
the Brighton Aquarium, and
also in that at the Crystal Palace.
The latest novelties are
the Proteus from the dark
caves of Adelsburg, axolotls
from Mexico, the mud-fish
(Lepidosiren annectans) from
the Gambia, and the telescope-fish
from Shanghai.
Some of these creatures are
of great interest from the circumstance
of their forming
the connecting-links between fishes and reptiles.
Fig. 325.—Proteus anguinus.
There are, therefore, now on view at the Brighton Aquarium specimens
of three species of animals possessing a high interest for naturalists and
others—not so much because their existence has been discovered in recent
times, as because they are illustrations of the great law of gradation which
exists in nature. Their position in the scale of organization is so intermediate
685between reptiles and fishes, that naturalists have not entirely
agreed as to the kingdom to which these ought to be assigned. Fig. 326
represents Lepidosiren annectans, which has gills covered by flaps, and not
exposed as they are in ordinary
amphibious animals;
and is provided with four fins,
or rudimentary legs, according
as the reader may choose
to call them. The creature’s
nostrils do not communicate
with the mouth, but are merely
two blind sacs, as in fishes.
The Proteus anguinus, shown
in Fig. 325, is an eel-like creature,
only met with in the subterranean
waters of the Grotto
of the Maddalena at Adelsburg.
It has four imperfectly
developed legs, and gills
reduced to mere fringe, while
there are lungs extending
nearly the whole length of
the abdomen. The optical
organs are entirely undeveloped,
being represented
merely by two specks. The
axolotl, Fig. 327, inhabits certain
Mexican lakes, and is
remarkable for preserving,
through the whole period of
its life, the gills for aquatic
respiration, which other amphibia
possess in the tadpole
stage only.
Fig. 326.—The Mud-fish (Lepidosiren annectans).
The mania for domestic
aquaria which was at its
height some years ago, and
the great popularity of public
marine aquaria wherever they
are properly managed, express
the real interest which
is felt in the varied forms of
animal life, of which the aquarium
affords the opportunity
of observing new and unknown
phases. The progress
of the science which treats of
the organization of the animal kingdom has made rapid strides during the
present century. Among the remarkable truths which have been acquired
is the fact of the unity of the plan which pervades the animal kingdom.
Each kind of animal has much in common with the kind above it, and
with the kind below it: a certain community of organization pervades the
whole, which is knit into one by the gradational forms which may be observed
686connecting, like links of a chain which cannot be broken, the more
defined modifications from each other. It is their position in the scale of
organization which, in the eyes of the philosophic naturalist, gives so much
interest to some of the forms of life which have been figured above.
Fig. 327.—The Axolotl.
687
Fig. 328.—Sorting, Washing, and Digging at the South African Alluvial Diamond-Fields.
GOLD AND DIAMONDS. — GOLD. — DIAMONDS.
It need hardly be said that gold and diamonds are named under nineteenth
century discoveries in relation to the newly-found fields which
have yielded these highly-prized substances in remarkable abundance.
This precious metal is met with in nearly all parts of the world, and
its splendid colour, high lustre, the ease with which it may be wrought,
and its property of ever remaining untarnished, have caused it to be greatly
esteemed for ornamental purposes from the earliest historical ages. No
doubt the store set upon gold is derived from its suitability for decorative
uses; and its comparative scarcity enhances the regard in which it is
held. Its use, as a standard of value, is justified by the general estimation
688in which it is held, and by the fact that the amount of labour required to
obtain the metal is on the whole tolerably uniform. It is one of the few
metals which are found in nature in the uncombined state, but its separation
from the materials with which it is associated requires the performance
of a certain amount of work, in whatever form the metal may occur. Its
general distribution is another advantage attending its selection as the
standard of value. It occurs in England and Wales; in Spain, in France,
in Hungary, in Piedmont, and in other parts of Europe; in various localities
in Asia; in both divisions of the New World; in the remaining quarter
of the globe, where it was obtained even in very ancient times, for South-East
Africa was probably the locality to which a naval expedition was
despatched by King Solomon—“they came to Ophir, and fetched from
thence gold.” Australia also has, in the last half of our century, yielded
much gold.
Gold is never met with in regular veins, but in primitive or igneous
rocks, or in deposits formed by the disintegration of these. In Australia
the metal is associated with quartz, in slate rocks geologically equivalent
to the Cambrian formations of England and Wales; and in California it is
also chiefly found in material which has been formed by the wearing down
of quartz and granite rocks. Before the discoveries in California and Australia
most of the gold in circulation was obtained from auriferous iron
pyrites. The first finding of gold in California occurred in September, 1847,
when a Mr. Marshall, the proprietor of a saw-mill on the Sacramento River,
observed some glistening grains among the sand in his mill-race. The news
soon spread, and the inhabitants of the town of San Francisco, then numbering
about two hundred persons, were greatly excited thereby. When
it became known that gold was really to be found, multitudes flocked to
California, the population of San Francisco rapidly increased, and at the
present day the city contains nearly a thousand times as many inhabitants
as it did at the time gold was first discovered. The annual value of the
metal found in California averaged about £23,000,000 for ten years after
1851; but this subsequently declined to less than half in 1872.
Sir Roderick Murchison, the distinguished geologist, pointed out the
great probability of the existence of gold in Australia many years before
the precious metal was actually found. It has, however, been stated that
gold was met with in Australia so long ago as 1788. Considering the mode
in which the metal occurs, it seems strange that the emigrants who occupied
the auriferous districts as agriculturists did not long ago discover the
riches which Nature had scattered over the surface of the soil. No doubt,
their attention was too much devoted to their sheep and cattle to notice the
glittering particles which might be seen in the water-courses, and it would
probably never enter their minds that the eagerly desired metal could lie
exposed to view on the surface of the land. But the announcement of the
discoveries in California induced men to look at the soil more attentively,
and in April, 1851, Mr. Hargreaves appears to have found at Bathurst the
first gold met with in Australia. Four months afterwards the metal was also
picked up at Ballarat, Victoria, and the gold-fields so discovered proved
even richer than those of Sydney.
The effect of this discovery on the colony of Victoria proved marvellous.
The population, which in 1851 was 77,000, had in 1867 become 660,000; in
the same period the land under cultivation expanded from 57,000 acres to
631,000, and the value of property rose enormously when the grazier’s estimate
of its worth was replaced by that of the miner. The authorities of
the colony from the first regulated the mining operations by enactments
689defining the rights of the miners to the “claims,” as the allotments of land
for working upon are termed; and thus disorder and lawlessness were
almost unknown. Fig. 329 will give the reader a notion of the appearance
of a miners’ settlement in the Australian gold-fields in the earlier period.
Fig. 329.—Gold Miners’ Camp.
The fundamental rocks in the colony of Victoria belong to the oldest
series of strata. They answer to the Silurian formation which exists in
Cumberland, Wales, and Scotland. Although the strata of the rocks are
much bent, and they have been worn down by the action of water, they are
as a whole but little altered, consisting chiefly of sandstones and shales.
These strata are interpenetrated by innumerable veins of quartz, which
vary in thickness from 1 16 in. to 150 ft. It is in these quartz veins that the
gold is seen in its original matrix. The metal is sometimes in the form of
grains or flakes, or in moss-like threads, embedded in the quartz; sometimes
in the form of well-defined crystals, sometimes in rough lumps or
nuggets. Fig. 330 shows three of the various modes in which the gold is
found disseminated through quartz. Overlying the more ancient rocks with
their auriferous quartz veins are various rocks of different ages; and as
these have been in part formed by the wearing down of the older rocks,
they also are in general auriferous, and contain the gold in detached pieces,
varying in size from particles of fine dust to the huge nugget, containing
2,280 oz., or nearly £10,000 worth of pure gold, which was found at Dunolly.
The soil, which has been formed by the disintegration of masses of auriferous
quartz, is full of gold, so that a patch of such soil 12 ft. square has
been known to yield 30 oz. of gold by a very rough kind of washing to the
depth of 1 ft. Soil of this kind has been carried down by rivers and streams
ages ago; and the lighter particles having been carried off by the water,
while the gold, from its greater specific gravity, remained at the bottom of
690the stream, the sands and gravel of these river-beds are very rich in gold.
In many instances the ancient water-courses have been entirely covered
by igneous rocks, such as basalt, which have flowed over the land in a
molten state. The gold-miner often finds his reward in burrowing beneath
these basalts and lavas, following the bed of the ancient river, and recovering
its long-buried treasures.
Fig. 330.—Gold in Rocks.
Fig. 331.—“Cradle” for Gold-washing.
The methods of carrying on the gold-seeking operations vary according
to the nature of the deposit which is worked and the resources of the miner.
The simplest, which was that most practised in the early days of the gold-fields,
consists in throwing into a tub several shovelsful of the surface soil,
and in pouring in water while the contents of the tub are stirred about with
a spade. The lighter matters are washed away, but the gold by its great
specific gravity remains behind. An improvement in this, but still a very
rude process, is practised by aid of the cradle, Fig. 331, which is merely the
trunk of a tree, hollowed out, and provided with transverse partitions and
ribs. The auriferous earth is thrown into the upper compartment, which
is then filled with water. The cradle is rocked, so that the water may
wash away all but the gold and the heavy stones. Any particles of the
former which may be carried out of the head of the cradle will be stopped
by the ribs which cross the lower part. Machines for puddling by horse-power
are now in use, and other contrivances have superseded the tub and
the cradle in surface-washing. The auriferous earth obtained by excavating
691the soil from pits is washed in a similar manner, as is also the material
reached by penetrating the deeper tertiary deposits, and by driving adits
or tunnels along the ancient river-beds beneath the layers of basalt.
A mode of washing accumulations of auriferous earths by streams of water
is employed where circumstances are favourable. A long inclined channel
is constructed, and lined with boards; or, when the natural inclination of the
soil requires it, a long trough is constructed and supported on trestles. The
trough is made of sawn boards, 1½ in. thick, in sections 12 ft. long, and it has
a width of about 1 ft., the sides being from 8 in. to 2 ft. high. The inclination
of the troughs is from 8 in. to 24 in. in 12 ft., and depends upon the abundance
of the water: the more water, the steeper is the slope. The bottoms
of the troughs are crossed by a number of transverse bars, which arrest
the auriferous particles in their descent. The sluice, or series of troughs,
may be from 50 ft. to several hundreds or even thousands of feet in length,
and the cost from £100 to £8,000. The earth is thrown in at the upper part
of the trough, and it is gradually washed down, the water being allowed to
flow in some cases by night as well as by day, but commonly in the day-time
only, as the troughs must be watched, to see that they do not become choked
up, and the soil washed out by the overflowing water. The run goes on
for six or ten days, and then the current is stopped for a cleaning-up, which
occupies from half a day to a day. For this operation the stream of water
is stopped, and quicksilver is used to dissolve the grains of gold from the
sand, &c., collected by the riffle-bars. The quicksilver is afterwards expelled
from the amalgam by heat, and the gold remains as a porous mass.
Sometimes, instead of shovelling the earth into the troughs, it can be
washed out of its position into suitable channels by means of a powerful
jet of water. This mode of working, which is termed hydraulic jet sluicing,
offers great advantages where the natural conditions admit of its adoption.
In this plan, instead of bringing the auriferous earth to the water, the
water is brought to the earth by a flexible pipe, like the hose of a fire-engine,
from a reservoir about 200 ft. higher, and the stream is directed upon the
material by a nozzle. This powerful jet of water is used to separate and
carry away the earth to the head of a system of channels and troughs, like
those already described. The hose has a diameter of 8 in., but the orifice
of the nozzle from which the water issues is contracted, in order to increase
the force of the jet. The hydraulic jet sluicing requires from three to six
men to work it, and the material of a hill can be carried into the sluices in
less time than a hundred persons could do it by spades. Immense quantities
of earth are removed in this way, and fatal accidents are not infrequent
from the falling masses burying the men who carry the pipe. The
force of the jet of water itself is another source of danger, for broken limbs
and even fatal injuries have often been caused by it. The number of accidental
deaths occurring in hydraulic jet sluicing operations in the colony of
Victoria is reported to average about 60 in a year. Material which has
been worked before often yields a considerable amount of gold when the
operations are repeated; and in localities favourable to the hydraulic jet
system, the work can be carried on with little labour. In this way three
men have been known to extract in one week from dirt washed for the
third time, gold of the value of £330.
The gold which is embedded in quartz and other minerals, as shown in
Fig. 330, is obtained by crushing the material in stamping machines, which
are usually constructed with logs of wood shod with iron. In another form
of crushing-mill two large cast-iron rollers are used instead of stampers.
692From the crushed material the particles of gold are extracted by amalgamation
with mercury, which is afterwards removed by distillation.
The richness of the Victoria gold-fields may be inferred from the fact
that, up to the year 1868, 36,835,692 oz. had been obtained, the value of
which is no less than £147,342,767. The total value of the gold then
annually obtained throughout the whole world is estimated at about 20
millions of pounds sterling. When gold was found so plentifully in California
and Australia, it was supposed by some that its value as a monetary
standard would be affected. This has not happened, although the prices
obtained for the metal by its producers were considerably lower in the
last decade of the century than about 1867. The total annual output of
gold throughout the world is of course variable, and no doubt there are
also variations in the demand; but, so far, the fluctuations have been
relatively small, and there has been no such depreciation by excess of
production as in the case of silver. Yet the increased production of gold
after the discoveries made about the middle of the century was beyond
precedent. It has been estimated that between 1850 and 1875 the total
value amounted to £600,000,000, showing an annual average twelve times
greater than that for the period between 1700 and 1850. Between 1875
and 1890 there was a falling off in the supply, the annual average becoming
only £20,000,000 in value. But since the last-named date there has
been a rise year by year, and at the close of the century the value of the
gold produced throughout the world in one year may not be less than
£40,000,000.
As already remarked, the distribution of gold is world-wide; and it
has happened in recent times, that just as one source of supply has
shown signs of failure, other fields have been discovered and have
attracted thousands of eager seekers to new regions. So, when the
Californian supply was falling off, there came the rush to Australia,
where easily worked alluvial deposits or rich veins continued for years
to reward the toil of the gold-finder, though in an ever-lessening degree,
until in 1886 or 1887 the centre of attraction was shifted. But at a later
period fresh discoveries in Australia again raised the productiveness of
that quarter; and still more recently, the announcement of the existence
of much auriferous deposit in the valley of the Yukon River (Klondyke),
and in various localities of British Columbia, drew thousands to desolate
and undeveloped districts, in spite of the extremities of hardship and
destitution that might be endured.
The discovery of 1886 takes us to South Africa, a region with which
also our next section is mainly concerned, and the scene of an activity
unprecedented in the annals of gold-mining. From circumstances immediately
connected with our present subject, the close of our century
finds public attention intensely occupied with affairs at the austral extremity
of the “dark continent.” The history of South Africa, from the
time when, in 1486, the tempest-driven Portuguese mariner, Bartholomew
Diaz, first struck its shores at the promontory he named the “Cape of
Storms” (Cabo Tormentoso), and when, eleven years afterwards, the
celebrated Vasco de Gama sailed round it on his memorable voyage to
India, is one which, in many respects, presents features of peculiar
interest. It is not our province to enter into details of these, but it may
be stated that the “Cape of Good Hope”—the more auspicious designation
which the King of Portugal substituted for that of Diaz—was,
towards the end of the seventeenth century, colonized by Dutch and
693some French settlers, and afterwards Table Bay became a regular port
of call for Dutch, English, and other ships trading to India. The Cape
was taken possession of by the British in 1795, but restored to the Dutch
in 1803, only to be three years after (1806) resumed by England, under
whose rule “Cape Colony” has since remained. The abolition of slavery
in all British dominions, enacted in 1833, was the occasion of great dissatisfaction
to the descendants of the Dutch settlers, who inhabited
isolated farmsteads, their possessions consisting chiefly of great herds of
cattle, tended by slaves. These people, or at least the majority of them,
resolved to quit the confines of British territory, and seek fresh fields and
pastures new in unoccupied regions north of the Orange River, so that
from 1835 to 1838 there was a continued “exodus of the emigrant
farmers.” The story of the following years, with its exciting events and
the vacillating policy of successive British Governments, must be perused
elsewhere: suffice it to say here, that the settlements of the “emigrant
farmers” had by 1854 established themselves into two separate States,
nominally recognising Great Britain as the “paramount power,” but
practically independent of it; for, at the last-named date, the autonomy
of “The Orange River Free State” was acknowledged, and two years
before that another section of the Boers, i.e. of the “emigrant farmers,”
who had settled beyond the Vaal River, was absolved from British
allegiance, and, restricted only by a claim of certain suzerain powers,
was constituted into “The South African Republic,” of which the precise
boundaries were at length determined by the “Convention of London”
in 1884. This territory is usually called for shortness the Transvaal,
and here in 1854 the existence of gold was first announced; but the Boer
authorities at once prohibited further prospecting, fearing, and perhaps
with reason, that the winning of the precious metal within their bounds
might disturb their pastoral quietude. The Boer character has been the
unique product of a race withdrawn for two centuries from contact with
European and civilized culture, living in widely separated dwellings with
scarcely other associations than cattle and enslaved blacks. The Boer
is described as of a type which draws away from the enterprising man of
modern times towards the primitive patriarch centred in his flocks and
herds: he hates innovations, and greatly distrusts strangers; he would
rather keep, in a box under his bed, any money he may possess than
employ it, or his own energies, in developing the immense mineral resources
of his territory, in which are included not only gold, but copper,
silver, lead, iron, and abundance of coal.
After some years the prohibition against the exploitation of gold in
the Transvaal was withdrawn, and several localities in the Republic
subsequently became small capitals of gold-mining industry. The most
notable were Leydenburg and Barberton, at which latter place as many
as 10,000 gold-seekers were congregated when the discovery of 1886
drew most of them away. These communities were formed almost entirely
by the influx of people from beyond the Boer boundaries, mainly,
of course, English-speaking people from the Cape Colony, Australia,
America, etc. Their operations were hampered by the Transvaal legislation,
and impeded by the absence of adequate means of communication,
which was a characteristic feature of the Boers’ unprogressiveness;
nevertheless, gold-mining has been pursued in some of these localities
ever since, though with varying fortune. What drew nearly all the gold-seekers
of the Transvaal and of adjoining regions at once to the north
694side of the Vaal River was the discovery there of real gold mines. This
was at a district within the Transvaal territory, named Witwatersrandt
(= White-waters-ridge), the designation which has been reduced by
abbreviation or affection to “The Randt”—or, anglice, the Rand.
It is singular that although the Randt district had been explored by
expert prospectors between 1877 and 1891, the outcrops of the auriferous
reefs entirely escaped their notice. But when the first hint of the existence
of these deposits was bruited abroad, it was the Kimberley men who
were foremost in surveying the spot. By the Kimberley men we mean
those who so soon had by lucky chance lighted in 1870 upon the rich and
apparently inexhaustible diamond mines, as related in our next section.
By the time of the announcement of gold-finds on the north side of the
Vaal River many of these men had become rich—very rich indeed. If
they had been so disposed they might then have returned to their
native countries with enviable fortunes, but it was just as the affairs of
their diamond companies had been settled by consolidation on a satisfactory
basis, and the spirit of discovery and adventure was still strong
upon them, that they resolved personally to explore the new El Dorado.
To a wild desolate region they proceeded, enduring there and on the
track thither the like discomforts they had experienced in their earlier
quest. But they took with them experts provided with all appliances for
ascertaining the prospective value of the alleged discovery, and, when
convinced of its reality, they purchased from the Boer possessors their
land at the price demanded, and it was not long before they had chemists
and engineers at work, having, at the cost of making their own roads,
had brought to the spot the necessary machinery and appliances. The
usual influx of workers, builders, speculators, etc., followed, and in a
wonderfully short space of time a town sprang up where in 1886 there
had been only a single poor farm. The town grew rapidly to the dimensions
of a city inhabited by 150,000 people. Its name is Johannesburg.
In his book on South Africa, the late Lord Randolph Churchill, describing
Johannesburg in 1891, says that it has much of the appearance of an
English manufacturing town, but without noise, smoke, or dirt. “The
streets are crowded with a busy, bustling, active, keen, intelligent-looking
throng. There are gathered together human beings from every quarter
of the globe, the English possessing an immense predominance. The
buildings and general architecture of the town attain an excellent
standard, style having been consulted and sought after, stone and bricks
the materials, corrugated iron being confined to the roofs, solidity, permanence,
and progress being the general characteristics.”
The Randt mines having drawn into the South African Republic great
numbers of enterprising workers, who have acquired wealth and built
cities, it would have been expected that they would have been permitted
to acquire the ordinary rights of citizenship. The Boers’ character, however,
has been manifested by their refusal of such rights, and by their
exacting grievous imposts from these Uitlanders (Out-landers, or
strangers), who, being for the most part of English race, are finding the
injustice too hard to be borne, and greatly strained relations between the
Transvaal and Great Britain have again supervened. Indeed, the situation
has become so serious that it is feared actual war may result, and that
is why, in almost the last year of our century, people are looking anxiously
at the position of affairs in South Africa.
The geological conditions of the Randt are these: the upper series of
695beds in the Karoo formation, which extends over the greater part of
South Africa, consist of quartzose strata, and in the district in question
these are much broken, faulted, and variously inclined. They are interstratified
with beds of sandstone and with the layers of gold-bearing
conglomerate, of which last there are several parallel to one another and
not far separated, ranging in their several thicknesses from 6 inches to
6 feet, the thickest being known as the main reef. These reefs form an
oval basin,—that is, they dip with varying angle towards a centre, and
crop out at their up-turned edges. Johannesburg is situated nearly 6,000
feet above the sea-level, on an elevated ridge, along which for 30 miles
east, and nearly the same westwards, the northern outcrop extends,
curving towards the south, while the southern edge of the basin appears
in the Orange Free State, where it has been traced for a distance of 130
miles. There a shaft, sunk to the great depth of 2,400 feet, found the
main reef with undiminished richness. The outcrop of the reefs stretches
east and west for 130 miles, and the distance between north and south is
30 miles. From such data it has been inferred that the reefs contain
altogether not less than 450 million pounds worth of gold. The conglomerate
of these reefs consists of rounded quartz pebbles (which
contain no gold), and pieces of sandstone and of argillaceous material,
the whole cemented together into a very hard mass by iron pyrites. This
last is the matrix in which the gold exists, in the form, for the most part,
of minute scarcely visible crystals. To a depth of from 50 to 150 feet, air
and moisture have acted on the pyritic matter, and the material of the
reef becoming in consequence easily disintegrated, has yielded by mere
mechanical treatment most of its gold, whereas by the same operations
on the underlying hard, tough conglomerate, only about half its gold
could be obtained. Hence, after breaking up the ore, the pyritic matter
is sorted out and transported to the stamp battery, reduced to powder,
from which about five-eighths of the contained gold is removed by quicksilver.
The residue is concentrated by washing in a special machine
called the “Frue vanner,” and the concentrates, after roasting in order
to oxidize base metals, are subjected to the action of chlorine gas, by
which the gold is converted into a soluble chloride, from the solution
of which it is precipitated by ferrous sulphate. The tailings, slimes,
and other residues are further acted on by a solution of potassium
cyanide, which dissolves the minute remaining particles of gold, and
from the solution the metal is obtained by electrolysis. By these supplementary
chemical processes the total of the gold recovered from the ore
is raised to 90 per cent. or more of all that chemical analysis shows to
exist.
When it is said that the reefs are arranged in a basin-like form, it must
be understood that this applies to their general disposition, for the
regularity of geometrical shape does not belong to geological basins.
There are considerable variations in the inclinations of the reefs: at
some places they are nearly vertical, but generally they dip towards the
centre at various angles, a slope between 25° and 45° being quite usual;
and the inclination becomes less and less the deeper they go, so that it
is presumed that the beds are level towards the centre of the basin. In
the Randt the vertical shaft is rather the exception, the entrance to the
mine usually following the inclination of the reefs, and the trucks of ore
are drawn up sloping rails. From the inclined adits horizontal galleries
are excavated right and left at various depths by which the main reef is
696worked, and there are cross cuts by which the reefs to the north and
south may be reached. The most active district of the Randt is that
which extends eastward of Johannesburg, where a long succession of tall
chimneys and winding headgears together with the other appurtenances
are visible. But there is nothing of a picturesque character about a gold
mine, more than is presented by the aspect of an ordinary colliery.
The importance of the Randt gold-fields does not consist in the actual
richness of the crude material, which indeed in places here and there
cannot be profitably worked,—in mining parlance, it is not “pay ore.”
It is rather the great ascertained extent of these gold-bearing beds and
the general persistence of their character throughout that give to the
Randt its unique character amongst metalliferous workings. This
contrasts with the comparative uncertainty attending the exploitation of
auriferous quartz veins, which occur in detached unconnected patches,
that often end suddenly where least expected. There are in the Randt
nearly one hundred companies working mines, and of these there are
many that pay very handsome dividends on their original capital. A few
pay 100 per cent., while a considerable number distribute 25 per cent.
and upwards; so that some of these Gold Companies are amongst the
richest and most influential financial houses in the world. The Randt is
second only to the United States in the quantity it adds annually to the
world’s production.
In ancient times, and down to a comparatively late period, the only
region from which were derived all the diamonds that found their way
to Europe, was India, where Golconda was long celebrated for the productive
mines in its neighbourhood, and for the high estimation in which
fine specimens of their yield were held. In the seventeenth century
these mines employed 60,000 persons, it is said; and in other districts
of India diamond-seeking has also been carried on from time immemorial.
A gradual decrease in the finds of Indian diamonds has long been
observed, and the supremacy the East had so long enjoyed as the
purveyor of gems was in the earlier part of the eighteenth century transferred
to another hemisphere. In 1727 the diamond was first discovered
in Brazil; or rather, we might say, was then first discerned there. For the
gold-seekers in washing the sands of certain Brazilian rivers had found
numberless specimens which they either threw aside as worthless, or,
seeing them prettier pebbles than the rest, used them as counters in their
card games; their true nature was not recognized, because the rough
diamond has by no means the attractive appearance of the cut and
polished brilliant flashing with refractive radiance. It must have been
these last, and not diamonds in their natural state, that presented themselves
to the imagination of the poet when he penned the line—
Or deep with diamonds in the flaming mine.
The announcement of some diamonds having been found in America
had no effect on the prices in the Indian market, but the exports that
soon after came from Brazil in great abundance quite changed the
conditions of the trade, for in the first fifty years their value was estimated
697at no less than £12,000,000 sterling. As already stated, the presence of
diamonds in Brazil was not recognized until 1727, and then by the
accident of one Lobo, an inhabitant of the gold district of Minas Geräes,
who had been in India and had seen rough diamonds there, observing
the resemblance; he took some of the Brazilian stones to Lisbon, where
their identity with the products of the Indian mines was established.
But the European dealers, alarmed lest this discovery should depreciate
the value of their stocks of Indian gems, spread a report that the
so-called diamonds from Brazil were but the refuse of the Indian mines
that had been sent to Brazil. This had the effect of stopping for a time
the sale of the Brazilian diamonds; but the traders in these were not
above taking a hint from their rivals—fas est et ab hoste doceri—for they
carried their diamonds to Bengal, and there sold them as Indian stones
at Indian prices. For nearly one hundred and forty years after this Brazil
was by far the most productive diamond region in the whole world, and
especially after 1754, when diamond-seekers congregated by thousands in
the very rich fields of Bahia, a district of Brazil. Nor have the places above
mentioned been by any means the only localities in Brazil where diamond-finders
have been at work; but the production has decreased and has lost
its relative importance by the South African discoveries that about 1870
caused an entire change in the diamond industry, and the high prices
of the Brazilian gems no longer capable of being maintained, the fall in
value has rendered the workings less remunerative than formerly. We
may now pass over with mere mention, discoveries of diamondiferous
districts in North America, Australia, and elsewhere.
While rejecting as entirely inapplicable and inexcusable by any stretch
of poetic licence the epithet flaming for the diamond mine, we must
question whether the word mine, that as the customary word we have
continued to use, does not convey an equally false notion of the nature
of the workings to which hitherto reference has been made. For these
in most cases are nothing more than holes, very much like gravel pits in
the side of a hill. The diamonds which have so far been in question are
usually found among alluvial sands or gravels, the water-worn fragments
of disintegrated rocks. These are in many cases carried down by rivers,
and the diamonds under such circumstances are very frequently accompanied
by gold; indeed, it is the search for gold that has in many cases
led to their discovery. In the dry season of the year, which extends from
April to October, the lessened currents of certain of the Brazilian streams
are diverted from their course into canals, so as to leave dry the bed of
the stream, and here the mud is dug out to the depth of six or eight feet
or more, and transported near the washing huts, these operations being
continued throughout the dry season. When this is over the digging is
necessarily interrupted by great volumes of water that fill the rivers and
streams, and the diamond-seekers devote their attention to washing the
mud that has been collected. About one cwt. of this is placed in a long
trough, and water is made to flow in, while the negro labourer stirs up
the mass with his hands, until the water runs off clear, all the particles
of mud having been washed away. The residual gravel is then very carefully
examined, stone by stone, and any diamonds found are handed to
the overseer, who watches all proceedings from an elevated seat. These
Brazilian diamonds are mostly of a small size: occasionally, but very
rarely, stones of quite exceptional value are found, but perhaps not one
in 10,000. Formerly when in the Brazilian fields a negro slave found one
698of 18 carats, or more (18 carats = 72 grains), he not only obtained his
freedom, but was rewarded with gifts, and for the finding of smaller
stones commensurate rewards were given. The value of a diamond
of the larger sizes depends upon so many adventitious circumstances
that it would not be easy for any one to state the money’s worth of an 18–carat
stone, but, considering too that the price increases in a more rapid
ratio than the weight, we may to some extent draw an inference from
the published values in 1867 of smaller Brazilian brilliants, perfectly
white, pure, and flawless, when one of 5 carats (20 grains) in weight
was priced at £350. As the rough diamond gives a brilliant of only
half its weight, we may from the above assume an 18–carat stone to
be worth in its finished state at least £1,000.
It may well be asked what are the qualities possessed by the diamond
which have caused it to be so highly valued as an adornment all the
world over; and here it will be proper to invite the reader’s attention to
the chemical as well as to the physical character of the diamond. The
most obvious and attractive quality of the cut brilliant is its unsurpassable
lustre, which is due to its high refractive power. In a section of our
article on light the subject of refraction has been dealt with, and an
explanation given of the index of refraction. That of the diamond is the
highest known, being 2·50 to 2·75; other precious stones have indices
ranging from 1·58 to 1·78; those of glass and of quartz are between 1·50
and 1·57. It follows from the known laws of refraction that the limiting
or critical angle is less for diamond than for other substances, as, for
example, glass, for the posterior surface of a diamond will totally reflect
all the light that falls upon it at any angle with the normal greater than
24°; glass will totally reflect only when the incidence is greater than
about 42°: hence the diamond reflects from its farther surface about 64
per cent. of rays that glass similarly situated would allow to pass outwards
without reflection.
Another property in which the diamond excels all other substances is
hardness. It is the hardest substance in nature; for a diamond will
scratch every other, but by none can it be scratched, except by another
diamond. Not but that by the application of a file the edges of a
diamond or brilliant may be notched and broken; but this would be
through sheer mechanical force tearing the substance, and would be a
test of brittleness, not of hardness. These two properties have not
unfrequently been confounded, as when it was foolishly prescribed as a
test for the genuineness of a diamond, that it should be placed on an anvil
and struck with a hammer. No doubt many good and valuable stones
have been sacrificed by this ignorant treatment. The hardness of the
diamond does not prevent its being reducible to powder when so required.
Again, diamonds are sometimes in such a condition of internal strain that
very slight shocks are sufficient to cause them to separate into fragments.
We read of diamonds that are suspected to be in this condition being
packed for transmission within raw potatoes. The extreme hardness of
the diamond secures it from all those accidental abrasions and injuries
to which softer materials are liable, so that it does not deteriorate by age
or use. It is unaffected also by any chemical substances.
In chemical composition the diamond is pure carbon, one of the most
commonly diffused of the elementary bodies, as it enters into the
constitution of the atmosphere, of all organic bodies, and of a vast number
of mineral substances. Carbon in a less pure form also occurs naturally
699as graphite, plumbago or black lead, and in other conditions comes into
ordinary use as already explained in our article on Iron. It was only
towards the end of the eighteenth century that the composition of the
diamond was demonstrated by the celebrated French chemist, Lavoisier,
who actually burnt a diamond in oxygen gas, and found the resulting
product to be carbonic acid gas, identical with that obtained by similarly
burning a piece of charcoal. Soon afterwards another French chemist,
Clouet, confirmed Lavoisier’s conclusion by producing steel from pure
iron and diamond heated together, an experiment of much significance
when considered in the light of the remarkable relation between these
substances, which is one of the latest discoveries of our century. It
should be observed that Clouet’s result implies a fusion of the diamond
as well as of the iron in the act of entering into chemical combination.
Like nearly every solid substance of definite chemical composition,
this pure carbon takes the crystalline form. The phenomena of crystallization
are of the highest interest and beauty, for in them we see
shapeless matter fashioning itself into definite and often perfect
geometrical solids, as if it had been wrought by the hand of some
mathematical artist. Every substance forms crystals of some one shape
when the conditions are identical, and one essential condition for any
crystallization is that the particles should be capable of free movement
in arranging themselves, and this condition can occur only when the
substance is in the state of liquid or of gas. Crystals are commonly
deposited from solutions when the solvent evaporates or is cooled down;
or they are formed when a fused substance solidifies. In either case the
crystals are the larger and more perfect as they are allowed the greater
time to form. Now, carbon in any of its conditions has been found to
be absolutely infusible and insoluble, and therefore the origin of the
diamond has long been a puzzle to scientific men, very diverse surmises
having been propounded on this subject. Some have thought it
was separated from carbonic acid by the action of heat, or of electricity;
others, that the carbon had been gasified by subterranean heat; others,
among whom were Newton and the German chemist, Liebig, believed
that heat had nothing to do with it, but that the crystals slowly separated
from vegetable matters (hydro-carbons) in the process of decomposition
under some unknown conditions; others, that the diamond crystallized
out from liquid carbonic acid, holding under pressure some unknown
form of carbon in solution; others, that carbon was ejected by volcanic
action in a fused state; and so on. We hope to show that the problem
has at length been solved, and how.
The shapes of the natural crystals of the diamond must not be
confounded with those of the cut brilliants. The most frequently met
with of the former is the octahedron, or eight-sided figure, such as would
result from two square pyramids joined base to base, the triangles forming
the sides of the pyramids being of such a height that the three
pairs of opposite points are equidistant one from another, so that the
octahedron enclosed in a cube would have an apex in the middle of each
surface of the cube. There are other shapes of diamond crystals, but
they are all related to the cube, that is, they are all obtainable from the
cube by successively slicing off edges and angles. The natural diamond
sometimes has as many as 48 faces formed by such a process. This will
easily be understood by the reader if he will take a cube of common soap
and perform on it these operations gradually with a sharp knife, taking
700care always to make the new faces he produces equally inclined to the
adjoining ones. He may begin by cutting off a tiny piece from one
corner of the cube, forming a small equilateral triangle; then let him do
the same at two opposite corners, and again at all the eight corners.
Then he should make the cuts larger and larger, always producing equal
sized equilateral triangles so long as these can be formed. In every case
he will have shaped out such forms as belong to diamond crystals.
Instead of this, he may pare off one or more edges of the cube, or he may
in various ways combine the two operations, and he will probably be
surprised at the variety of forms producible in this manner, all derived
from the original cube and all representing possible forms of natural
diamonds, and indeed those of any substance that crystallizes in the
cubical system. A model of the diamond octahedron can be readily made
from the description already given, and the whole series of operations
will constitute an elementary but very instructive lesson in the science
of crystallography.
Diamonds are liable to occur with every imaginable distortion, so as to
be scarcely recognizable by their external form. A very pure smooth
uncut diamond, belonging to the Rajah of Mattam in Borneo, is shaped
exactly like a pear, two inches in length. By the way, battles have been
fought for the possession of this gem, and it is said that,£200,000 was
vainly offered for it. The diamond, notwithstanding its hardness, splits
with comparative ease in certain planes, and by such cleavage (a property
common to all crystals) the octahedral form commonly emerges. It
was not until the middle of the fifteenth century that the art of cutting
the diamond into regular facets was practised, and this can be done only
by the aid of diamond powder, prepared by crushing fragments and
faulty stones in a hard steel mortar. The first operation is to split the
stone by its natural cleavage, and the rough facets so produced of two
diamonds are ground together until they are quite smooth. The grinding
of other facets and the polishing are effected on horizontal discs of
steel making 2,000 revolutions per minute, and overspread with diamond
powder mixed with olive oil.
The external surface of the diamond in its natural state is often very
rough, the stone being always coated with a more or less opaque crust,
so that its translucent interior is concealed or veiled; but when the
reflection from its inner surfaces pierces this veil it glows as if lighted
from within, giving that peculiar appearance which is called its “fire.”
The surfaces of the diamond crystals are very often curved instead of
being flat, and the dodecahedral shape, when this is the case, takes on an
almost globular appearance. Diamonds of all colours are found, as well
as the highly esteemed colourless stones. Yellow ones of various tints
are frequent,—orange, brown, and pink are not very rare; but red, green,
blue, and black are almost unique, at least in a condition to form large
and perfect gems, and are accordingly much prized. The black diamonds
found in Borneo are so hard that ordinary diamond powder has no effect
whatever upon them; they have to be manipulated with their own dust.
The nature of the substances that impart these colours to the diamond
has never been made out; they must be excessively small in quantity.
When a diamond is burnt in air or in oxygen gas by aid of a large burning
glass or otherwise, an extremely minute quantity of ash remains, and
this often retains the shape of the stone, in the form of a most delicate
network; and of the composition of the ash, this much has been made
701out: it contains silica and iron. We shall find that the presence of the
last named element, although but in the merest trace, is not without
significance.
The purely utilitarian uses of the diamond are few, but of importance.
The most familiar is in the glazier’s tool for cutting glass, and in
connection with this we may mention a fact not generally known, namely,
that though any point of a diamond will scratch glass, it is only by a natural
point of the crystal, and that point of a certain shape, that glass can be
cut. Another kind of diamond, valueless as a gem, has been turned to
good account in Major Beaumont’s invention, described in our section
on Rock Drilling Machines, to which the reader is referred. Minute
diamonds are employed for writing on glass, for very fine engraving,
etc.
Having now said sufficient about diamonds in general to give the
reader an interest in the subject, and yet but little more than was needed
to impart the information necessary for following the further development
of the theme, we approach the discoveries in this connection which
have specially distinguished our century. We must transfer the reader’s
attention to South Africa, and if he can refer to any recent map of that
region, particularly to one showing its physical features, it will be of
advantage.
In 1867 some children, playing near the banks of the Orange River, found
what they thought to be merely a pebble prettier than the rest. A neighbour
seeing the stone in the children’s possession, obtained it from their
mother for a trifle. It passed through several hands, and was bought at
last by the Governor of the colony for £500. The discovery shortly afterwards
of other diamonds in the same locality attracted numbers of persons
to the district, and especially to the banks of the Vaal River, which speedily
became the scene of a great search for diamonds. Though this search was
confined to merely the surface of the soil, it was attended with considerable
success, and many fine diamonds rewarded the diligence of the eager
seekers. One of the most remarkable stones for its great size, which
equalled that of a walnut, was discovered by a Kaffir. When this gem had
finally reached the hands of Messrs. Hunt and Roskell, of London, its
value was estimated at no less than £25,000. News of these discoveries
having spread, a rush set in for the diamond-fields of the Vaal River, and
the banks of this stream soon presented an animated spectacle. Europeans
flocked to the spot, London jewellers sent agents, and the inevitable Jews
appeared on the scene to purchase the precious gems from the lucky finders.
It turned out that many of the larger stones had a slightly yellow tinge,
varying in different specimens from the palest straw to a decided amber
colour, and, as this detracted greatly from their value, no little disappointment
and loss were sometimes experienced when the gems came to be
sold in London and Paris.
One of the first settlements which sprang up on the banks of the Vaal
River was a place called Pniel, of which the reader may form some idea
from Fig. 332, which is copied from a sketch actually taken from the windows
of Jardine’s Hotel. It was then only a little straggling village, chiefly
of wooden sheds or corrugated iron erections, with but two or three more substantial
structures. The diamonds which were found in this neighbourhood
were obtained from gravel which lay on the slopes of the hills rising from
the river. The mode of conducting the search for diamonds in these gravels
was simple enough. The first operation was the washing of the material,
702in order to remove sand and dirt, and this process was usually performed at
the margin of the river, where the gravel was brought down in carts and deposited
in a suitable place, at which a cradle was erected. The cradle was
simply a strong wooden framing sustaining sieves of wirework or perforated
metal, placed one above the other, those at the top having the largest
meshes, so that the lowest would only permit sand or very small pebbles to
pass through. The cradle was capable of receiving a rocking movement, and
while the gravel was thus sorted, water was freely poured on the uppermost
layer, so that the stuff was in a short time thoroughly cleansed and
sorted. When this had been accomplished, the gravel was thrown in successive
lots on a table, at which the digger sat and rapidly examined it for
diamonds by help of a flat piece of wood or iron (see Fig. 328). The larger
gems were readily detected, and indeed could be picked out from among
the pebbles on the sieve before the stuff was thrown on the sorting-table.
Crystals of quartz, which sometimes glisten among the mass, often excited
groundless delight in the bosom of the inexperienced worker.
Fig. 332.—Pniel, from Jardine’s Hotel (c. 1870).
On the payment of certain fees, the digger obtained a “claim,”—that is,
he acquired the right of working an assigned portion of the soil. But if
the claim had been left unworked for a week, it might be, in mining parlance,
“jumped”—that is, any person might take possession of it, or jump
into it, on procuring a proper licence.
Since the first rush of diamond-seekers to the river-banks, the stones
were abundantly found elsewhere, namely, at the “dry diggings,” where
the soil, dug out with a pick or shovel, was sifted first through rough
sieves, afterwards through sieves having fine wire meshes The sieve, in
such cases, was often suspended by thongs of hide between two upright
poles, in the manner represented in Fig. 333. The miner was thus enabled
to swing the sieve rapidly about, until the sand and dirt were separated,
when the remaining gravel was emptied on the sorting-table in the manner
before described. As the idea was formerly entertained that diamonds lie
only on or near the surface of the soil, the early miners seldom penetrated
more than a foot or two beneath the surface. But it was discovered that,
so far from it being true that diamonds are present in superficial deposits
only, the finest stones are met with at considerable depths to which no
defined limit can be assigned; thus in sinking a well large diamonds have
703been found at 100 ft. below the surface. When these facts became known,
many of the abandoned claims were worked over again down to a depth
of 30 ft. or 40 ft.
Fig. 333.—Sifting at the “Dry Diggings” (c. 1870).
The rapid rise of localities under such conditions may be illustrated by
the case of Du Toit’s Pan, which is the centre of a dry-digging district,
and grew in a wonderfully short space of time from nothing to be a town
hiving several large hotels, two churches, several public billiard-rooms, a
hospital, and a theatre. In 1871 the claims at this place, each 30 ft. square,
sold at prices varying from £1 to £50–-the person who worked a claim
paying also a small monthly sum for the licence. But those who were
lucky enough to have obtained the first possession of the claims at another
famous dry-digging locality, named Colesberg Kopje, at the cost of only
the licence at 10s. per month, must have been still more fortunate, and have
realized an enormous percentage on their investments; for, four months
afterwards the ruling prices at the last-mentioned place were £2,000 and
£4,000 per claim. This great increase in value cannot be wondered at, if
the accounts related of the value of the diamonds found here are true. For
instance, it is stated that one individual, who just before the great rush
had bought a claim for £50, found in it diamonds worth £20,000. Colesberg
has become a populous town, with good buildings and regularly
laid-out streets, while a great camp of tents and other temporary structures
still surround it on all sides.
At all the towns above-mentioned newspapers were published, relating
chiefly to matters interesting to the miners—giving, for example, lists of
“finds,” with the names of the lucky finders. It is curious that the term
“diamondiferous” has, in these localities, come to be used as a general
term denoting excellence of any kind. Thus, when it is desired to apply
704an epithet of superlative praise to a pickaxe or to a piece of furniture,
this significant adjective is made use of; and a salesman in the diamond-fields
will not hesitate to speak of diamondiferous coats and trousers!
Fig. 334.—The Vaal River, from Spence Kopje (c. 1870).
It will be seen that the early diamond-seekers at the Cape followed
very primitive methods, by simply washing in sieves the gravel and sand
shovelled out of the river banks; and indeed, it was only when, about 1871,
they began to dig deeper that their working seems entitled to be called
mining. The “dry-digging” operations began at the since famous Du
Toit’s Pan, by the circumstance of a Boer farmer finding to his great
surprise diamonds sticking in the walls of his house, which had been
built of mud. When the locality of this mud was examined by digging,
more diamonds were found; and when the excavation was continued
downwards, still more. At this place and at four others, all within a
circuit of less than four miles diameter, have been developed the richest
diamond mines in the world, throwing into the shade the produce of all
the river gravel washings; and what is still more remarkable, showing no
signs of exhaustion after nearly thirty years of working, but rather the
contrary. The locality soon presented a scene of the most active
industry, and it was not long before the town sprang up which has since
become celebrated all the world over—Kimberley, the diamond capital.
Kimberley is situated at the northern part of the British territory known
as Cape Colony, not far within its boundary, and about 14 miles from
the Vaal River, in Lat. 28° 43´ S., Long. 24° 46´ E. It lies in a north-easterly
direction from Cape Town, at a distance of about 550 miles. When
the existence of diamonds at the Cape became known, a great influx of
strangers seeking fortune set in to a land that had failed to offer the
attractions to colonists that America and Australia did. Before the
705establishment of the overland route opened a more direct way to India,
China, and Australia, Cape Colony owed whatever importance it had to
its position as a provisioning and coaling station for ships and steamers.
As a British settlement it was little regarded, and its somewhat somnolent
condition would have been deepened by the opening of the Suez Canal
in 1869, had not the diamond discovery in that very same year brought
about a great change. But the early diamond-seekers found their land
of promise a wilderness without roads and without habitations, for the
development of civilization did not then extend far from the coast. It
is true, that here and there, at great distances apart, a few primitive
missionary stations might be found, like that of Pniel shown in one of
our cuts, which also represent the inhospitable aspect of the country. One
cannot but admire the pluck of the adventurers, who, though unversed
in their quest, encountered in its prosecution prolonged toils and many
hardships. But they were young men, and their perseverance gained its
reward. They came from all parts: from Britain, from America, from
Australia, from Germany, even from Russia.
The finding at Du Toit’s Pan, and at contiguous places, of diamonds
at some depth below the surface of the soil, led to geological examinations
of the district, which ultimately resulted in discoveries of the
highest interest and importance, as will now be explained, with first a
few words about the external features of the country.
A traveller directing his steps northward from the sea-shore at almost
any part of the southern coast of Cape Colony will be faced by several
successive ranges of mountains, or what will appear to be such, running
more or less parallel to the coast, and of no great elevation. When he has
reached the summits of these heights he will not find corresponding declivities
on the northern side, but nearly level plains, bounded northwards by
other similar ranges. Supposing him to set out at a point, say, 150 miles
east of Cape Agulhas (the most southern point of Africa), he will, about
50 miles from the shore, have reached the top of the third of the great
escarpments which rise up like the stages of a gigantic terrace, and having
thus gained the ridge of the Black Mountains, he will see one of these
almost level plains stretching before him a breadth of 80 miles, for the
most part arid and inhospitable, with a much greater length east and
west, and bounded on the north by a portion of the range of elevations
that in an almost unbroken line runs through Cape Colony to Delagoa
Bay nearly parallel with the coast, at a distance from it between 100 and
150 miles. This extensive plain is known as the Groot Karoo (Great
Karoo),—karoo being the generic name for such plains in South Africa.
After crossing the Great Karoo, our traveller, on mounting the last far-reaching
step of the Brobdignagian staircase, may find himself on the
summit of the Nieuveldt Mountains, at an altitude of nearly 10,000 feet
above the sea-level, attained in several widely separated stages within a
distance of 140 miles. From the summit of these elevations there is
no descent by terraces northwards, but the high tableland or plateau
stretches away for hundreds of miles, descending by only a gentle slope
towards the Orange River, but maintaining an average altitude of nearly
6,000 feet, and extending far beyond the Orange River towards the
Equator. Kimberley is situated about 50 miles north of the Orange
River, and 4,042 feet above the sea-level.
It was soon observed that the Karoos had common geological
characters, consisting in a certain series of shales, coal, limestones, etc.,
706and this series naturally came to be called the “Karoo formation,” just
as we in England speak of the Wealden formation, etc.; and it was found
that it extended over a greater part of Central South Africa, covering an
area of at least 200,000 square miles, with an estimated thickness of 5,000
feet. The reader need not imagine that a boring nearly a mile in depth
had to be made for the ascertainment of this last dimension, if he will
remember what has been said in the last paragraph about escarpments
of the rocks looking everywhere towards the coast. There is reason to
believe that these beds were originally the sedimentary deposits of a
vast fresh-water lake, or inland sea, far back in geological times. But
here we need only concern ourselves with the development of the Karoo
beds about Kimberley. There the ground is covered by a sandy soil of
a red colour, for it contains much iron. Below this there is a layer of
decomposed basalt, also containing much iron, its thickness varying from
20 to 90 feet. This lies upon a bed of very combustible shale, with
carbon and iron pyrites, 250 feet thick, which from its great development
here is known as Kimberley shale; then, after a conglomerate stratum
10 feet thick, is found a very hard compact rock, resembling hornblende,
extending 400 feet downwards, and resting on another hard rock of
quartz, also 400 feet in depth. These beds are nearly horizontal, but
dipping a little towards the north. In speaking of them collectively we
may use the local term of the miners and call them “the reef.”
Now, there are a few certain spots near Kimberley, and two or three
elsewhere, in which the strata forming “the reef” are not found, but
something quite different. These may be compared to large dry wells,
extending vertically downwards to unknown depths, which have been
filled up with matters from below. They are called pipes, but they
are uncommonly large ones; for though of a somewhat irregular circular
or oval shape, their diameters range from 200 to 500 feet. Nor must it
be supposed that the enclosing reef presents itself as a smooth wall, as
the name “pipe” might suggest. These pipes are true diamond mines.
They are believed to have been formed by an eruptive action originating
from below at a great depth, and this was not by the escape of red-hot
lava or other molten rocks, but by that of steam or other gases. It is
known that the eruptive forces acted from below, for the edges of some of
the strata are seen in places in the walls of the reef that surround the
pipes to be turned a little upwards. It is known that the erupted matter
was not molten lava or rock, for the shale and other strata show none of
those changes of character near the pipes which would have resulted
from igneous action, and for the same reason the gas or steam that
escaped by these pipes could not have been highly heated. It must
therefore have forced its way through the strata by enormous tension or
pressure, and this either at one terrific outburst or possibly by the
gradual enlargement of smaller volcanic chimneys. These blow-holes
are filled with a mixture of subterranean débris, as if mud had been
forced up from below, carrying with it an extraordinary variety of rock
fragments and crystallized minerals. These are embedded in a mass of
a bluish-green colour much resembling indurated clay (but nearly as hard
as ordinary sandstone), and this on long exposure to the weather
crumbles down to a yellow friable substance. More than eighty different
kinds of minerals of the volcanic class have been found in this breccia, as
it is termed by geologists, and it is remarked that these fragments could
not have been exposed to any great heat, for their edges show no signs of
707fusion. There are also embedded in the agglutinating substance large
masses of the surrounding strata, sometimes having an area of several
thousand square feet, and these are called in miners’ parlance “floating
reef.” The cementing material is named “blue ground,” and the same
when crumbled down by exposure is known as “yellow ground.” These
colours are due to oxides of iron, which in the unaltered ground give
the blue-green tint, being lower oxides; but are converted by absorption
of oxygen into yellow and higher oxides. The upper part of the pipes is
filled to a depth of about 70 feet with “yellow ground,” produced by the
penetration of atmospheric influences. Blue ground and yellow ground
alike contain diamonds, and the yield of these is pretty regular at all depths
in the same mine (some have been explored down to nearly 2,000 feet),
although it varies considerably from one mine to another, and in some
the east side is often richer than the west. Thus in one load (1,600 lbs.)
of ground from Du Toit’s Pan, in 1890, the quantity of diamonds found
averaged less than 2 grains (0·5 carat), while Kimberley yielded 1·25 to
1·5 carats (5 to 6 grains). It is singular that the stones from mines quite
close together are so distinctly different in character, that the Kimberley
merchants can tell at once the source of any particular parcel. This
would indicate that the blue mud was not forced up the several pipes at
one and the same time, carrying with it diamonds from one birthplace.
The existence of the diamondiferous pipes is pointed out by no
indication on the surface, which is covered nearly uniformly with the red
sandy soil already spoken of; although indeed the site of the Kimberley
mine was marked by a slight elevation, and that of Du Toit’s Pan by
one of the depressions there called pans, which, at least in the wet
season, are receptacles for surface water. The Wesselton mine, which
was found only in the last decade of the century, about a mile from Du
Toit’s Pan, also showed a surface depression, and that had been utilised
as a depositing place for dry rubbish. At a later period the “Leicester
mine” was accidentally discovered 40 miles away. At Jagersfontein,
in the Orange River Free State, 60 miles from the Kimberley mines,
is another pipe which yields the finest diamonds of any, commanding
prices nearly the double of those paid for the De Beers and Kimberley
gems, being in fact their nearest commercial rival. The proprietorship
of the Kimberley group having in 1889 become united in the hands of one
company, known as the “De Beers Consolidated Mines,” this company
is able practically to control the diamond market, as it has sometimes
turned out in a year as much as 3 million carats of diamonds, which sell
for about £3,500,000. Up to the end of 1892, 10 tons of diamonds had
been derived from these mines, representing a value of £60,000,000
sterling. In 1895, the De Beers Company sold diamonds to the amount
of £3,105,958, the total expense of working for that year being £1,704,813,—the
net profit was £1,401,145. The effect of consolidating all the
Kimberley diamond interest into the De Beers Company has been to
give an almost complete monopoly to this last, which has however found
it advantageous to restrict its production to an annual output of about
£3,000,000 in value, as the putting of a larger quantity of diamonds on
the market would cause lowering of their price, and a diminution of the
profits all round. The reason is, that though the world at large annually
spends between 4 and 4½ million pounds sterling in the purchase of
diamonds, yet it would not by a reduction in their price be induced to
spend proportionately more. The company are sufficiently supplied by
708only two of their mines, the Kimberley and the De Beers, the expenses
of working these being also relatively smaller than is the case with the
others. It may be of interest to compare the quantities of diamonds
that have so far been produced from the world’s greatest fields, leaving
out Borneo, the Ural Mountains, Australia, etc., as comparatively
insignificant. Estimated produce of India, from the remotest period, 10
million carats; of Brazil (since 1728), 12 million carats; of South
Africa, in only 19 years, 57 million carats.
At the time of the discovery of the Kimberley mine (July 1871) it was
divided into about 500 claims, each 31 feet square, and between these
were roadways across; but when the claims were excavated to a depth
of 100 feet or more the roadways became unsafe, and, the “blue
ground” underneath them being too tempting always to be left for
their support, they began to fall in, and the mine was often threatened
with ruin from this cause. The state of things became still worse when
the unsupported walls of the “pipe” itself began to collapse, so that by
1878 a quarter of the claims were buried in the ruins of the reef. These
falls continued, and although very large sums were year after year
expended in removing the fallen reef, the cost amounting in 1882 to
2 million pounds sterling, it was found at last that very few of the claims
could be regularly worked, and when in 1883 a tremendous fall of
250,000 cubic yards of reef took place, covering half the area of the mine,
it became necessary to adopt another mode of working, namely, a regular
system of underground mining. Vertical shafts were sunk at a considerable
distance from the pipe itself, and tunnels from these carried
through at different levels, with a system of galleries so arranged that all
the “blue ground” is removable without danger to the miners. The
whole mine is illuminated by electric lights, and the different kinds of
labour are carried on by distinct sets of workmen, some of whom drill
holes for the reception of dynamite cartridges, others shovel the material
into trucks, others again wheel the trucks along tram lines, which
converge to a space where their contents are discharged into skips holding
four truck loads, in which they are hoisted to the surface at about
the rate of 400 loads per hour. This goes on day and night, the miners
working in three shifts of eight hours each. About 8,000 persons are
employed, 6,500 of whom are blacks.
Fig. 334a is a sketch section of the Kimberley diamond mine, approximately
to scale, and a glance at this will elucidate the foregoing description.
The thick vertical and horizontal lines show the positions of the
shafts and galleries that have at various times been excavated, the lowest
gallery being connected with a shaft a considerable distance from the
pipe, towards the right, but out of the range of the sketch. The fringed
lines at the top, with dates, give some idea of the forms of the excavations
until the final fall of reef that determined the resort to subterranean
working.
Fig. 334a.—Sketch Section of the Kimberley Diamond Mine.
When the “blue ground” has come to the surface, how are the
diamonds to be extracted from the hard mass? how can a stone of a few
grains weight be found amongst 1,600 lbs. of miscellaneous matter—a
thing perhaps not larger than a peppercorn in four cubic feet of compact
material? The “blue ground” is spread out on levelled and carefully
prepared areas called “depositing floors,” and there, after a few months’
exposure, all but the very hardest pieces crumble down, the atmospheric
action being accelerated by turning the material over with harrows, and
709by occasional waterings. The “blue ground” from the De Beers mine
requires at least six months of this treatment, and it contains a certain
proportion of refractory lumps that would not disintegrate in perhaps less
than two years. These lumps are coarsely crushed between rollers, and
the fragments are spread over slowly moving tables, from which any
larger diamonds are picked off; the fragments left go through smaller
crushers, and are subjected to still greater concentration. The depositing
floors of the De Beers mine are laid out as rectangles, 600 yards long
by 200 yards wide, each holding about 50,000 loads. They occupy
several square miles, and as the “blue ground” spread upon them is
always one of the most valuable assets of the company, the quantity of
it forms an important item in the balance-sheets, and the amount that
can be realized from it can be estimated with sufficient closeness, on
account of the nearly uniform distribution of the diamonds. Thus in
June 1895, the 3,360,256 loads then on the floors were put down as
equivalent to nearly 1 million pounds sterling. When the “ground,”
thoroughly weathered, has become yellow and friable, it is transferred to
the washing machinery, by which about 99 per cent, of the original non-diamondiferous
material is removed, and, thus concentrated, the gravel is
together with the mechanically crushed material submitted to the action
of a machine called the pulsator, where the gravel is first assorted into
sizes by being turned about within an inclined iron cylinder perforated
with several stages of round holes of diameters successively of 2, 3, 4
and 6 sixteenths of an inch. The pieces that are too coarse to pass
through the largest holes are taken to the sorting house direct; but the
stones that have passed through the cylinder drop according to their
sizes into four separate sieves called at Kimberley jigs, from the well-known
mining term jigger, applied to a man who washes ores in a sieve.
The several jigs into which passes the now assorted gravel have screens
710with meshes corresponding to the holes in the cylinder; and by a very
ingenious arrangement the concentration is carried to the point at which
the diamonds can be individually picked out. The “jigs” themselves
do not move, but all over the meshes of the screen is spread a layer of
leaden bullets, which prevent a too rapid passage through the screens,
while the material is kept moving in water, by that liquid pulsating or
emerging in quickly succeeding gushes from below the meshes, and thus
carrying off the lighter matters, while those of greater specific gravity,
including the diamonds, work their way downwards between the bullets
and through the meshes, and are received in boxes which are periodically
carried to the sorting house.
When the now much concentrated diamondiferous gravel reaches the
sorting house, the remaining operation consists merely in picking the
diamonds out. But simple as this operation is, it has to be conducted
systematically. In the sorting house are long tables covered with
plates of iron, and placed in a good light. Upon these is thrown the wet
gravel, but not promiscuously; the different sizes being set apart, the
sorter spreads out the heap before him with a flat piece of zinc, picks out
the diamonds and drops them into a small box. Only white men in
whom confidence can be placed are allowed to deal with largest sized
material, for this offers the strongest temptation to purloiners, as in this
of course the most valuable stones are met with. This material, after the
first search, is submitted to the scrutiny of another person, to see that
no diamond has been overlooked; but the smaller assortments are
examined by blacks, who are closely supervised by white men. The
value of the diamonds occasionally sorted out in a single day may reach
£10,000.
At the diamond mines little trust is reposed in the honesty of the
blacks. Below ground and above ground they work under the constant
surveillance of white men, and they live in “compounds” which are
spacious areas—perhaps of 20 acres in extent—enclosed by lofty iron
fences, and containing long rows of corrugated iron erections divided
into rooms, each appropriated to a score of natives. Food, etc., is
supplied from a store at less than ordinary prices, and the company find
fuel and water gratis, and provide a well equipped hospital and medical
attendance. There are swimming baths, and ample recreation grounds
for dancing, etc. The natives of each of the many tribes keep by themselves
apart, and follow their own fancies. They receive good wages,
and some of them save money. They are not allowed out of the
“compound” or the mine, except to work on the depositing floor, which
they do under guard. They accept their restrictions voluntarily, making
agreements for a certain term, three months being the least. Those
who leave, as many do to spend their earnings, often “not wisely but too
well,” usually return. The depositing floors are surrounded by fences
7 feet high, unscalably and impenetrably armed with barbed wire;
and as here robbery would have the readiest chance, where the largest
stones might be met with, extraordinary precautions are taken, watch
and ward being maintained by day and by night. Not more vigilantly
did Cerberus keep the entrance of Pluto’s domain, nor the wakeful dragon
guard the golden apples of the Hesperides, than the patrols observe the
depositing floors. At night powerful electric searchlights are made to
play across the enclosures, so that unauthorized movements can scarcely
escape detection. Besides these provisions against theft, the laws of the
711Colony prohibit any attempt at illicit dealing in diamonds, under a
penalty of two years’ penal servitude.
The maximum penalties for contravention of the Diamond Laws are,
however, much more severe, and that to an extraordinary degree. Thus
any unlicensed dealer is liable to a fine of £1,000, or fifteen years’
imprisonment, or both. And the authorized dealers are required to keep
a most minute record of all their transactions, to send a copy of it every
month to the head of the police, and to produce it when required. It is
needless to say that extraordinary precautions are taken to prevent the
native workmen from secreting diamonds. And any person even finding
a diamond, and neglecting to report the circumstance to the proper
quarter at once, is liable to the pains and penalties above mentioned.
The “blue ground” was at first supposed to be the original home of
the diamond, within which it had somehow taken its shape. But no
satisfactory explanation was forthcoming as to the state of the carbon
before its solidification into the crystalline form. The more general
opinion has been in favour of a volcanic origin due to very high
temperature; and although the “blue ground” itself is clearly not the
ordinary erupted matter of volcanoes due to igneous fusion, the geology
points to the district having been the scene of very active and extensive
volcanic energies at more than one remote period, for the bed of the
Karoo inland sea has been several times covered by level sheets of
molten matter extruded somewhere from below; but not through the
“pipes,” which were blown out ages afterwards. The strata of basalt
and of hornblendic mineral, which extend horizontally over great areas
in the Karoo formation, are of igneous origin, as are also some nearly
vertical dykes of trap rock, about 7 feet wide, that are found
traversing the “blue ground” in certain directions. These intrusive
dykes are of course more recent than the formation of the blue ground,
and that is itself later than the production of the pipes. The fact of
many fragments of crystals being found in the “blue ground” does not
comport with the theory that supposes it to be the matrix; and besides
this, many of the diamonds show scratches, and as these are producible
only by other diamonds, it would appear that they must all have travelled
in company, some part of their journey at least.
Carbon in any form is quite infusible at the highest temperature we
have hitherto been able to produce, although an incipient softening under
the influence of the electric arc has been suspected. Professor Dewar,
an English chemist, basing his data on analogies with other substances,
and on purely theoretical grounds, has calculated that the melting
temperature of carbon is near 3,600° C. (6,512° F.), and that it cannot
remain in a liquid state at a temperature exceeding 5,527° C., when its
vapour would have a tension equivalent to a pressure of 15 tons on the
square inch. So far as these deductions are correct, both the melting
point of carbon and the boiling point of its liquid must lie within the
range of temperature expressed by 3,600° C. and 5,527° C. The most
intense heat we can produce is that developed in the electric arc
discharge, and an eminent French chemist and metallurgist, M. Moissan,
by employing special arrangements and very powerful currents, has thus
been able to obtain in his “electric furnace” a temperature estimated at
3,500° C., which nearly approaches the lower of the above-mentioned
limits, and he has thereby produced many new and unexpected chemical
combinations of refractory elements. Among the most striking of his
712results is the formation artificially of real crystalline diamonds. He found
that carbon is freely dissolved by several of the metals in fusion at the
temperature of the electric furnace. When the carbon separated from
the metals, as they cooled and became solid, it was always in the
condition of graphite. The carbons of the electric poles were readily
attacked by molten iron, and it was from the solution of carbon in iron
that Moissan prepared his diamonds. The fact of carbon thus combining
with iron was of course no discovery, as the reader already knows; and
the resulting combination was found, on allowing the metal to cool, to be
simply cast iron, the greater part of the carbon separating out in the
graphitic form. But M. Moissan, having studied the conditions of the
Kimberley mines, and recognizing the probability of the diamonds having
taken their origin at very great depths, where the pressure due to the
weight of superincumbent strata would be immense, was struck with the
idea of pressure being in some way a factor in their formation; and it
occurred to him that the carbon might separate from its liquid condition
in the iron in the crystalline, and not in the graphitic form, if the
solidification could be effected under great pressure. The apparently
insurmountable difficulty of applying an enormous pressure to a small
quantity of molten iron (half a pound) yielded to the experimenter’s
ingenuity. He took advantage of the circumstance that cast iron at the
moment of solidification expands, a property upon which depends its
use for many purposes. If then the fused mass were suddenly cooled on
the outside, we should have a shell of solid iron enclosing a nucleus of
still fluid metal, which, on cooling in its turn, would tend to expand, and
by so doing would exert a great pressure within the shell by which it
was confined. At first Moissan plunged his glowing crucible into cold
water, but a method of more rapidly cooling it was to immerse it in
melted lead. It seems a strange proceeding to cool the crucible by
surrounding it with hot metal, yet the difference of the temperatures was
sufficient to produce the desired effect, the cooling contact of water not
really operating on the intensely heated body, which becomes separated
from the liquid by a coating of steam. When the mass of iron was
dissolved off, diamonds of all kinds were found in the residue, and, though
extremely small, some crystals were perfect in shape and colour; every
variety that occurred in the mines being found reproduced in tiny size.
There was also some graphite in the residue. Many more crystals of
“pure water” were obtained by the lead-cooling than by the water-cooling,
as the former process gave some flawless cubes and octahedra.
The largest of the set was only 1 50 inch across, and although of perfect
form when first extracted, within the course of three months it had
spontaneously split up into fragments.
There was evidently no danger of M. Moissan’s manufacture of
diamonds from coke causing consternation at Kimberley; though it
would not be without interest to speculate upon the consequences had
the French savant achieved the greater triumph of turning out carbon
crystals in every respect equal to the productions of nature’s own
laboratories. What a drop there would have been in the shares of the
De Beers Mines Consolidated! What heaviness of heart would have
fallen upon those great ladies who exult in the exclusive possession of
priceless tiaras and precious necklaces flashing with the resplendent
gems! From a scientific point of view, M. Moissan’s fabrication of even
those minute crystals, which so soon spontaneously crumbled into fragments,
713is a distinct and valuable success; for, notwithstanding their
diminutive size and instability, they show us that art has so far succeeded
in imitating the processes of nature, that some of her secrets have been
revealed. Though we know the exact chemical composition of all kinds
of crystallized minerals, very very few of these have we been able to
imitate artificially. Nor is this to be wondered at; for nature’s resources
are immense compared with ours: she can command temperatures
unlimited by which to form her solutions or liquefactions; prodigious
pressures to keep them close; and time immeasurable—geological time—in
which to let them cool, and their particles freely coalesce into
geometric forms. Human agency, being obviously unable to reproduce,
even on the smallest scale, such conditions as attended the deposition
and slow cooling of the earth’s crust, may not hope to rival the products
of the planet’s prime. So the fair owners of the earth-born gems may
possess their souls in peace, free from any fear of the chemists’ crucibles;
and the Kimberley Diamond Companies are not likely to suffer panics
from the results of scientific researches, and probably will continue to
pay their handsome dividends for time indefinite.
But curiously enough, a discovery of the latest years of our century has
revealed the existence of diamonds in a region not mapped by the most
advanced of geographers—a region which indeed cannot be defined by
degrees of latitude and longitude. In the recesses of an unquestionable
meteorite—one of those celestial lumps of iron of which mention has been
made in the earlier pages of this volume—real diamonds have been found.
These quite resembled the products of M. Moissan’s experiments, being
extremely small, but including clear and perfectly shaped crystals,
associated with black ones, and also with much graphite in more or
less definite forms. So very limited, however, could be the quantity of
diamonds obtainable from this hitherto unsuspected source, that even if
they rivalled in quality the finest stones from the South African mines, it
might be difficult to form a “Company” for their exploitation. Still,
there is the possibility of some one falling in with a little meteorite containing
some mature full-sized carbon crystals, and such a one might be
considered equally fortunate with the finder of the famous Australian
nugget “Welcome” (£25,000). The association of diamonds with the
ferruginous matter of the “blue ground” in the Kimberley pipes, their
crystallization out of iron in M. Moissan’s experiments, and their presence
in iron meteorites, would seem to point to special relations between the
two elements, iron and carbon. Some of these relations are exemplified
in another way by the profound modification effected in the physical
properties of iron, by its combination with a very small quantity of
carbon, as in some kinds of steel; or again, by the differences between
white cast iron and grey cast iron, as determined by the condition of the
carbon in each.
714
Fig. 335.—Portrait of Sir Humphrey Davy.
NEW METALS.
The chemistry of the nineteenth century can boast of a series of discoveries
more brilliant and more numerous than ever belonged to any
other science within a like period. And the advantage to the world must
have been great, for chemistry more directly than any other branch of knowledge
ministers to the useful arts and promotes the comfort and well-being
of society. The science itself, as it now exists, is almost the creation
of the present age. But its recent developments cannot be here discussed;
nor, of the immense number of new products with which it has enriched
the world, can more than a very few be brought under the reader’s notice
in the remaining pages of the present work. Among the most striking of
the remarkable series of discoveries by which Sir Humphrey Davy penetrated
the mysteries of matter was the isolation of the alkali metals—a
circumstance which marks an important era in the history of chemistry.
That the alkalies were oxides of unknown metals had indeed been previously
surmised by chemists, from the fact of their behaving like metallic
oxides in neutralizing and combining with acids to form the class of compounds
called salts. All attempts to decompose these alkalies had proved
715fruitless until Davy separated the metal potassium from potash, in 1807.
When, however, this alkali had once been proved a compound, more
correct ideas were introduced into chemical science; the nature of other
alkalies and earths was explained in like manner, and new and powerful
re-agents were placed in the hands of the chemist.
Davy first obtained potassium by exposing to the action of the voltaic
current a fragment of potash which had become moist on the surface by
exposure to the air. The battery was formed of the then unprecedented
combination of two hundred pairs of 6–inch plates on Wollaston’s plan,
which was constructed for the Royal Institution of London. The heat produced
by the passage of the current fused the potash, and globules of metallic
potassium were separated at the negative wire. This method yielded
the metal in very small quantities only, and at a great cost. Gay Lussac
and Thenard soon afterwards found that potassium could be obtained more
cheaply and in greater abundance when fused potash was made to flow
over iron-turnings heated to whiteness in a gun-barrel, and the hydrogen
and potassium vapour were passed into a cooled receiver, in which the
latter body was condensed. The metal is now obtained by heating potassium
carbonate with charcoal. For this purpose it suffices to heat crude
tartar in a covered vessel from which air is excluded. The tartar is first
calcined in a crucible until all combustible vapour has been driven off.
The charred mass, which now consists of potassium carbonate mixed with
finely-divided carbon, is then broken into lumps and quickly introduced
into a wrought-iron retort, which is heated in a furnace to nearly a white
heat. A receiver in the form of a flat iron box, 12 in. long, 5 in. wide, and
¼ in. deep, is adapted to the neck of the retort, and is kept cooled by the
application of a wet cloth on the outside. The potassium thus obtained is
not pure, and it must be distilled in an iron retort, as otherwise a powerfully
detonating compound is apt to be formed by a portion of the metal
combining with carbonic oxide.
Immediately after his discovery of potassium Davy obtained sodium in
the same manner, and Gay Lussac and Thenard also procured it by the
same process they used for the sister metal. Sodium is now extracted on
the manufacturing scale for use as an agent in the reduction of two other
metals, of which we shall have to speak. A mixture of dried sodium carbonate,
powdered charcoal, and chalk is heated in wrought-iron cylinders,
about 4 ft. long, 5 in. internal diameter, and ½ in. thick. The chalk takes
no part in the chemical action, but is added in order to give the sodium
carbonate when it fuses a pasty consistence, and thus prevent the separation
of the charcoal. A number of these iron cylinders are set in a reverberatory
furnace; but they are coated with fire-clay and enclosed in earthenware
tubes, to prevent their destruction by the intense heat. To one end of
each cylinder a receiver is adapted, of the form and dimensions already described
for potassium. The other extremity is closed by an iron plug, luted
with fire-clay. When the charge in a cylinder is exhausted, a fresh one is
introduced by removing the plug, taking out the residue, and inserting a
new supply of the mixture made up in a canvas bag. The operation is
therefore continuous, and the metal obtained is nearly pure, as sodium
does not exhibit the same tendency as potassium to form compounds with
carbonic oxide.
Potassium and sodium are extremely soft metals; they are lighter than
water, upon which they float, at the same time rapidly decomposing that
compound by displacing half the hydrogen, which is set on fire by the heat.
716The instant a piece of potassium touches the surface of water, a violet
flame bursts forth; but with sodium no flame appears unless the metal is
dropped on warm water, or prevented from swimming about. Since these
metals are thus capable of displacing hydrogen from its combination with
oxygen at ordinary temperatures, it follows that they must have a powerful
affinity for oxygen; and, indeed, they can only be preserved in rock oil,
for they rapidly combine with the oxygen of the air. The great attraction
of these metals for oxygen, and for chlorine and other similar bodies, induces
the chemist to employ them for separating such bodies from their
combination with other metals. Sodium is generally employed for this
purpose, as being far cheaper than potassium.
Among the sixty-nine elementary or undecomposable substances which,
variously combined, constitute the whole material of our planet, so far as
we are acquainted with it, no fewer than fifty-six are metals. Of these
fifty-six metals very few are found in a free or uncombined state, like the
gold described in the last article. On the contrary, the whole of the
metallic elements of the globe, with insignificant exceptions, exist in nature
in a state of combination with one or more of the other thirteen non-metallic
substances. In this condition they form the stony masses which are
termed the ores of the more common metals, and they constitute also the
earths, the metallic bases of which were, until recent times, unsuspected
and unknown. Davy followed up his discovery of the metals of potash
and soda by experimental demonstrations that the earths alumina, magnesia,
and others, were really oxides of metals; and when the nature of
these substances had once been established, chemists soon devised means
for readily obtaining their metallic bases in an isolated form. The new
metals which have been thus isolated all deserve the attention of the
chemist; and the general reader will probably also regard with interest
the processes by which two of these new metals, for which practical applications
have been found, are extracted, and the properties which have
caused them to be produced on the commercial scale. These are aluminium,
the metallic base of common clay; and magnesium, the metallic
base of common magnesia, and Epsom salts, and a constituent of dolomite,
or magnesian limestone.
Aluminium was first isolated by Œrsted, in 1827, by decomposing its
chloride by means of potassium. The chlorine leaves the aluminium to
combine with the potassium, and thus the former is set free. Wöhler
effected some improvements in Œrsted’s process, and he first obtained the
metal in malleable globules. It is, however, to Deville that we are indebted
for the invention, in 1854, of a process which admitted of application
on a manufacturing scale. He obtains chloride of aluminium by
mixing alumina (the oxide of the metal) with powdered charcoal made into
a paste with oil, and heating the mixture in a tubular earthenware retort,
like those sometimes used in the manufacture of coal-gas, while a current
of dry chlorine is made to pass through the vessel. The charcoal combines
with the oxygen, forming carbonic oxide, a permanent invisible gas; and
the aluminium unites with the chlorine, giving rise to aluminium chloride,
which, being volatile, sublimes into a chamber lined with glazed tiles, in
which it condenses as a yellow translucent mass. The metal is reduced
from the chloride in the following manner: A tube of hard glass, about
an inch and a half in diameter, is placed over a furnace, or chaffing-dish,
as shown in Fig. 336, where D C is the tube, and G G an iron pan for containing
the red-hot charcoal. Into the part of this tube marked E, about
717half a pound of dry aluminium chloride has previously been introduced,
and is kept in its place by plugs of asbestos. A current of dry hydrogen
gas, perfectly free from air, is passed through the tube; the gas being
generated in the vessel, A, and in B passed over some substance which
removes from it all moisture. The aluminium chloride is then gently
heated by placing red-hot charcoal beneath it, so that any hydrochloric
acid it may contain may be expelled. A long narrow porcelain tray, or
“boat,” containing pieces of sodium, F, is then introduced into the tube;
and, the current of hydrogen being still maintained, heat is applied to the
part of the tube containing the sodium, and the aluminium chloride is
made to distil over by a regulated heat. As it passes over the sodium, it
is reduced with a vivid glow. The aluminium is set free, and collects in
the tray with the double chloride of sodium and aluminium which is produced
by the reaction. The tray is removed and more strongly heated in
a porcelain tube through which a current of hydrogen is passing, and the
metal is thus obtained in globules.
Fig. 336.
Messrs. Bell, of Newcastle, undertook the manufacture of aluminium by
a system founded on this process. The first step is the preparation of pure
alumina, which may be obtained by igniting ammonia alum, or by precipitating
from a solution of alum free from iron, or from sodium aluminate
made from the mineral called bauxite. The precipitate of hydrated
alumina, mixed with charcoal and common salt, is made into balls and
dried. These balls, which are about as large as an orange, are placed in
upright earthenware retorts, which are heated to redness, while a current
of dry chlorine is passed through them. The volatile double chloride of
aluminium and sodium distils over, and is condensed in chambers lined
with earthenware. This substance is mixed with powdered fluor-spar, or
with cryolite (itself a compound of aluminium), which serves as a flux; and
small pieces of sodium are interspersed throughout the mixture. The proportions
are ten parts of the double chloride, five of fluor-spar, and two of
sodium. This mixture is thrown upon the hearth of a reverberatory furnace,
and the doors are shut to exclude air. A very intense action occurs:
the chlorine, quitting the aluminium, seizes on the sodium, and their combination
is attended by an enormous increase of temperature. The fused
aluminium is run off from the furnace together with the slags which are
produced by the operation. In this way, with a furnace having a hearth
16 ft. square, about 16 lbs. of aluminium can be obtained in one operation.
Rose, the eminent German metallurgist, prefers to obtain aluminium
from cryolite, which is a compound of sodium, aluminium, and fluorine,
found in large quantities in Greenland. It is powdered and mixed with
718common salt, and with the mixture a certain quantity of sodium cut into
small pieces is uniformly mingled. The whole is thrown into a heated
crucible, previously lined with a fused mixture of cryolite and salt, and
more of the same mixture is poured upon the contents of the crucible,
which is then covered and exposed to a red heat for two hours. The
aluminium generally collects into buttons, which may be easily melted
together by heating them in a crucible with common salt.
It will be obvious, from the preceding account of the processes of extracting
aluminium, that the cost of the metal must depend upon that of
sodium; and the same remark will apply to the case of magnesium. It is
interesting to observe how the price of the alkaline metals has decreased
as improved processes have been devised, and as the scale of production
has increased with the commercial demand for the article. Prepared by
Gay Lussac and Thenard’s process, these metals were produced in but
small quantities, and were sold at £5 per oz. When the mode of reducing
them by charcoal came into operation, the price fell to 30s. per oz.;
and the researches of Deville so far improved the processes, that in 1854
sodium could be procured for 5s. per oz. Mr. Gerhard, of Battersea,
subsequently manufactured sodium, so that it can now be retailed at less
than 1s. per oz. The price of aluminium before Deville’s investigations
was about 24s. per oz., but now the metal can be purchased at about one-eighth
of that cost. [1875.]
Aluminium is a white malleable metal, in colour and hardness not unlike
zinc. Its colour is not so white as that of silver, as it has a marked bluish
tint. It can be rolled into very thin sheets, and by rolling it becomes
harder and more elastic. It can also be drawn into fine wire. It is remarkably
sonorous, and a suspended bar gives out a clear musical note
when struck. Perhaps no property of aluminium more strikes a person,
who examines the metal for the first time, than its lightness. It is, in fact,
only two and a half times as heavy as water, while zinc is seven times,
silver ten and a half times, and gold more than nineteen times as heavy as
water. It retains its lustre in dry or in moist air for any length of time,
and at all ordinary temperatures. It is not acted upon by nitric or sulphuric
acids, but is attacked by hydrochloric acids and by alkaline solutions
with great energy. It has great rigidity and tenacity, and can be
turned, chased, and filed with the greatest ease, and without clogging the
tools. In the Paris Exhibition,[15] M. Christofle showed spoons and forks and
a cup made from it; and it may be mentioned, as showing the hardness
and strength of the metal, that the cup could be allowed to fall on a stone
pavement without being indented. The metal gives a good impression by
casting; and by striking under a die, some admirable medals have been
produced in it. Aluminium has hitherto been chiefly used for ornamental
articles, and for purposes where lightness and rigidity are desirable, such
as in the tubes of telescopes, opera glasses, beams of balances, &c. Its
unalterability and admirable working qualities have also caused it to be
used for cheap trinkets and ornaments—such as watch-cases, bracelets,
combs, seals, penholders, candlesticks, &c. It is, however, incapable of
receiving the lustrous polish of silver, as it has a decidedly blue tint, so
that it will probably never replace silver for ornamental plate; but it would
be a good material for egg and mustard-spoons, as it is quite unaffected by
the sulphur compounds which so readily tarnish silver. It has been suggested
that if aluminium could be procured cheaply enough, “its hardness,
lightness, and incapability of rusting would render it admirably adapted for
719the helmets and cuirasses of the cavalry; it would make splendid field-guns,
as strong as the present ones, and not one-third of their weight;
and, in sheets, it might serve as an incorrodible roofing, far lighter and
more durable than zinc. It would admirably replace copper, if not silver,
for the purpose of coinage. A crown-piece in aluminium would hardly
weigh more than a shilling in silver, or a piece the size of a penny about
as much as a copper farthing. The same qualities of lightness, hardness,
and incorrodibility also excellently fit it for the beams of delicate balances,
and for the small weights used by the analytical chemist. It would make
admirable utensils for the more delicate operations of cooking—replacing
the copper ones, which render pickles and soups so poisonous. It is extremely
sonorous, and would make capital bells.”
Some difficulty in working the metal has occurred from the want of any
suitable solder. This difficulty has been overcome by electrolytically coating
the metal with copper at the place where it has to be united with others,
and then soldering the copper in the ordinary manner. Aluminium readily
forms alloys with copper, silver, and iron. The alloys with copper vary in
colour from white to golden yellow, according to the proportion of the
metals. Some of these alloys are very hard and possess excellent working
qualities. The alloy of copper with 10 per cent. of aluminium, which is
called aluminium bronze, has been manufactured by Messrs. Bell in considerable
quantities. It is made by melting a quantity of very pure copper
in a plumbago crucible, and when the crucible has been removed from the
furnace, the solid aluminium is dropped in. An extraordinary increase of
temperature then occurs: the whole mass becomes white hot, and unless
the crucible be made of a highly refractory material, it is fused by the heat
developed in the combination of the two metals, although it may have
stood the heat necessary for the fusion of copper.
The qualities of aluminium bronze have been investigated by Lieut.-Col.
Strange, who finds that the alloy possesses a very high degree of tensile
strength, and also great power of resisting compression, its rigidity,
or power of resisting cross strains, is also very great; in other words, a bar
of the alloy, fixed at one end and acted on at the other by a transverse
force tending to bend it, offers great resistance,—namely, three times as
much as gun-metal. An advantage attending the use of the alloy for many
delicate purposes is found in its small expansibility by heat; it is therefore
well adapted for all finely-graduated instruments. It is very malleable, has
excellent sounding properties, and resists the action of the atmosphere. It
works admirably with cutting tools, turns well in the lathe, and does not
clog the files or other tools. It is readily made into tubes, or wires, or
other desired forms. The elasticity it possesses is very remarkable; for
wires made of it are found to answer better for Foucault’s pendulum experiment
than even those of steel. These admirable qualities would seem
to recommend the alloy for many applications in which it might be expected
to excel other metals. It appears, however, that the demand for it has not
met the expectations of the manufacturers, and the production has been
somewhat diminished of late, although it is used to some extent for chains,
pencil-cases, toothpicks, and other trinkets. When more than 10 per cent.
of aluminium is added to the copper, the alloy produced is weaker; and if
the proportion is increased beyond a certain extent, the bronze becomes so
brittle that it may be pulverized in a mortar.
The metal magnesium was first prepared, in 1830, by the French chemist
Bussy, by a process similar to that by which Deville obtained aluminium.
720Bussy heated anhydrous magnesium chloride with potassium in a porcelain
crucible; and when the vessel had cooled, and the soluble residue had been
dissolved out by water, the metal was found as a grey powder, which could be
melted into globules. The recognition of the metal as the base of magnesia
is, however, due to Davy. About a quarter of a century after Bussy’s discovery
Deville having shown that sodium could be substituted for potassium
in such reductions, the metal became more cheaply producible, and soon
afterwards Bunsen and Roscoe pointed out its value as a source of light.
Mr. Sonstadt devoted himself to the elaboration of a method of working
Deville’s process on the large scale, and he succeeded in establishing a
company in Manchester for the manufacture. The process as carried on
at the company’s works in Salford is thus described in the “Mechanics’
Magazine,” 30th August, 1867:
“Lumps of rock magnesia (magnesium carbonate) are placed in large
jars, into which hydrochloric acid in aqueous solution is poured. Chemical
action at once ensues: the chlorine and the magnesium embrace, and the
oxygen and carbon pass off in the form of carbonic acid. The result is
magnesium in combination with chlorine, and the problem now is how to
dissolve this new alliance—to get rid of the chlorine and so obtain the magnesium.
First, the water must be evaporated, which would be easy enough
if not attended with a peculiar danger. To get the magnesium chloride
perfectly dry it is necessary to bring it to a red heat; but this would result
in the metal dropping its novel acquaintance with chlorine and resuming
its ancient union with oxygen. To avert this re-combination, the magnesium
chloride whilst yet in solution is mixed with sodium chloride (i.e., common
salt), and thus fortified, the aggressions of oxygen whilst drying are
kept off. The mixture is exposed in broad open pans over stoves, and when
sufficiently dry, the double salt is scraped together and placed in an iron
crucible, in which it is heated until melted, whereby the last traces of water
are driven off. It is then stowed away until required in air-tight vessels,
to prevent deliquescence. Here comes in that curious metal, sodium, also
discovered by Davy. Five parts of the mixed magnesium and sodium
chlorides, mingled with one part of sodium, are placed in a strong iron
crucible with a closely-fitting lid, which is then screwed down. The crucible
is heated to redness in a furnace, and its contents being fused, the sodium
takes the chlorine from the magnesium. When the crucible has been lifted
from the fire and allowed to cool, the lid is removed and a solid mass is
discovered, which, when tumbled out and broken up, reveals magnesium
in nuggets of various sizes and shapes, bright as silver.”
The crude metal also presents itself in the crucible as small grains, and
even as a black powder. The whole is carefully separated from the refuse;
it is purified by distillation in a current of hydrogen gas; and it is afterwards
melted and cast into ingots. Magnesium is a very light metal, its
specific gravity being only 1·743; that is, it is only one and three-quarter
times heavier than water. When heated in the air it takes fire, and is
rapidly converted into the oxide, magnesia. In the form of wire or of
narrow ribbon, it burns easily in the air, producing a light of dazzling brilliancy,
which among artificial modes of illumination is rivalled only by the
electric light. This is the chief use at present made of the metal. Lamps
have been contrived for burning the wire in such a manner as to obtain a
steady light, the wire being pushed forward at a regulated rate by clockwork.
The magnesium light is rich in the rays which act upon sensitive
photographic plates, and it has been successfully employed in obtaining
721photographs of dark interiors, such as vaults or caverns, and for the exploration
of mines and other dark places. The brilliancy of the firework displays
which can be produced by magnesium far surpasses that obtainable
by any other material used by the pyrotechnist. In such exhibitions
balloons are sent up having burning magnesium attached to them; and the
metal in the state of filings is also mixed with other materials. But magnesium
is still a very costly metal, and while the firework-makers find it too
expensive for common use, they complain that its brilliancy in occasional
displays dulls by contrast the effect of the ordinary fireworks, with which
the spectators are no longer satisfied.
Magnesium wire is not produced by drawing, as the metal is not ductile.
The wire is formed by a method identical with that used in the fabrication
of the leaden rope for making bullets (p. 330); that is to say, the metal is
forced in a heated and softened state through a small opening in an iron
cylinder. The intensity of the magnesium light has been measured by
Bunsen and Roscoe. They say that 72 grains of magnesium, when properly
burnt, evolve as much light as 74 stearine candles burning for ten hours,
and consuming 20 lbs. of stearine. Lamps in which magnesium may be
steadily burnt are made by Mr. F. W. Hart, of London. In the more
elaborate forms of these lamps, there are springs and wheels for pushing
forward the magnesium ribbon, or a strand of magnesium wire, into the
flame of a spirit-lamp; while at the same time the magnesium wire is made
to revolve on its axis, in order to overcome its tendency to bend down,
which would be a great disadvantage when the light is used for optical
apparatus. But for ordinary purposes a much simpler arrangement suffices:
the magnesium ribbon or wire is coiled on a drum, from which it is drawn
off by passing between two little rollers, which are turned by hand. The
wire or ribbon is drawn off the drum by the rollers, and pushed forward
through a guiding tube, which brings it into the apex of the flame of a
spirit-lamp. In this simpler form of lamp the rate is, of course, directly
dependent on the person who turns the winch of the feeding-rollers; but
in the automatic lamp there are appliances for adjusting the rate; the
suitable speed must be first found by trial, and then the apparatus is to be
regulated accordingly. By means of these lamps photographs can be taken
as quickly as with sunlight, on account of the abundance of chemically-active
rays given out by the burning magnesium. It has been found that
an equivalent of magnesium, in combining with oxygen, liberates a larger
amount of heat than the equivalent quantity of any other metal, not excluding
even potassium. Magnesium forms alloys with several other metals,
such as lead, tin, mercury, gold, silver, platinum. All these alloys are
brittle, and have a granular or crystalline fracture. They are too readily
acted on by air and moisture to be of any service in the arts. The alloy
of 85 parts of tin with 15 of magnesium is hard and brittle; its colour is
lavender, although both constituents are white, or nearly so; and it decomposes
water at ordinary temperatures. Both metallic magnesium and
aluminium furnish useful re-agents to the scientific chemist. The latter
metal, when fused, dissolves boron, silicon, and titanium, and on cooling
deposits these elements in the crystalline form, this being the only known
process for artificially preparing them in the crystalline state.
Since the above paragraphs were written, the price of sodium has been
further greatly reduced, and it can now (1890) be purchased in bulk at
about 4s. per lb. This cheapness has brought the substance into use for
the reduction of other metals and one consequence has been a great fall in
722the price of aluminium. At Salindres, in France, the process of obtaining
this metal that has been described on page 587, has been in use for many
years, during which considerable quantities of aluminium have been
produced, the output for 1882 being stated as 5,280 lbs. Aluminium has
lately been prepared by a company at Wallsend-on-Tyne from cryolite,
a mineral which is found only in Greenland, but occurs there in great
abundance. Cryolite is a double fluoride of aluminium and sodium, and
the processes for its reduction consist in fusing it with common salt in a
reverberatory furnace, drawing off the mixture into an iron vessel, and
stirring into the fused mass a certain quantity of sodium. This produces
a violent action, on the cessation of which the slag is poured off, and the
metallic aluminium is found as a “button” at the bottom of the converter.
For obtaining a purer metal, the fusion is made in crucibles, and the
sodium is added in two operations without removing the crucible. The
yield of aluminium is about 8 per cent. of the weight of cryolite, and three
parts of sodium are required to furnish one part of aluminium. Another
large manufactory of aluminium is in operation at Oldbury, near Birmingham.
There is a special difficulty in the metallurgy of aluminium, arising
from the fact of the qualities of the metal being much deteriorated by the
presence of a very small amount of foreign matters such as iron, silicon, &c.,
at the same time that no process has been found for purifying the product
from these substances. If the aluminium is to be pure it must be so
prepared at the first. Electrolysis has been proposed as a means of
reducing the compounds, and obtaining the metal free from admixtures.
Experiments seem to show that the dynamo-electric machine may be
applied to this purpose, as well as to the reduction of sodium compounds,
when certain practical difficulties arising from the chemical energies of
the liberated substances have been overcome. What is called the
“electric” furnace has been successfully used in the production of
aluminium bronze. It is a rectangular iron box, 5 feet long, 1 foot deep,
and 15 inches wide, with electrodes formed of rods of carbon 30 inches
long and 3 inches in diameter. It is charged with a mixture of 25 parts
of corundum (native crystallized oxide of aluminium), 12 parts of carbon,
and 50 parts of granulated copper. This is covered at the top by lumps
of charcoal, and a lid is fastened over the whole. The current from a
powerful dynamo is sent through the carbons, and in about ten minutes
the copper is melted, when the electrodes, at first only a few inches apart,
are moved to an increased distance, and the strength of current increased.
The corundum is reduced, the aluminium alloying itself with copper, and
the oxygen combining with the carbon to form carbon monoxide, which is
driven off. The resulting alloy is cast into ingots, its percentage of
aluminium ascertained, and then it is melted with enough copper to
produce aluminium bronze (page 719). The price of aluminium, which
was as already stated about 3s. per ounce in 1875, has been so much
reduced that the metal may now (1890) be purchased for 11s. or 12s. per lb.
We may therefore expect to see wider applications of its excellent qualities.
Though the price per lb. is still much higher than that of copper-–22 or
more times as much—the metal is so much lighter that a lb. of aluminium
occupies nearly 3⅓ times the space of a lb. of copper, so that, taking bulk
for bulk, aluminium is only about seven times as dear as copper. [1890.]
When first introduced by Deville, in 1854, aluminium cost £20 per lb.;
but its prospective value for application in the arts was recognised, and
in two or three years afterwards it was put on the market at 40s. per lb.
723It was then, as already remarked, applied to many purposes where lightness
is desirable, such as for the tubes of telescopes, opera-glasses, the
mounting of photographic lenses, &c. And in 1888, when the production
of sodium had been cheapened and applied to the separation of
aluminium, the price of the latter metal fell to 18s. per lb. In the meantime,
the cheap electricity of the dynamo caused attention to be again
directed to the original electrolytic method; but many difficulties in
detail had to be overcome in applying this process on the commercial
scale. At length the sodium process was superseded; and by the
beginning of 1890, a Swiss company was producing aluminium at 11s. per
lb. In the course of the following year they succeeded in bringing the
price down to 2s. per lb.; and again three years later, namely at the
beginning of 1894, they could offer the metal at 1s. 7d. per lb. The
conditions required for effecting this great reduction were found in driving
the dynamo machinery by water-power, and in an abundant supply
of cryolite at moderate cost. This cheapness of production at once
placed the Swiss company in the position of being the largest and most
successful aluminium manufacturers in the world, so that in 1892 they
had realised a net profit of £21,563, paying their shareholders 8 per cent.,
and, further, in 1893, the net profit was half as much again, and the
dividend was increased to 10 per cent. A British aluminium company
has recently been formed in London for acquiring the rights of working
all the processes of the successful Swiss company, purchasing outstanding
English patents, amalgamating with certain existing companies, and
for working the bauxite deposits in Ireland, &c., &c. There is every
reason to believe that an important result of this enterprise will be a still
further reduction in the price of this metal, and consequently a great
extension of its applications. And now (September, 1895) we have already
heard of a further reduction in the price of this metal, which, at the
present time, can be purchased in bulk for about 1s. 6d. per lb.
724
Fig. 337.—Portrait of Mr. Thomas Hancock.
INDIAN-RUBBER and GUTTA-PERCHA. — INDIAN-RUBBER. — GUTTA-PERCHA.
Researches into the history of the human race in remote ages have
revealed the fact, that before man knew how to extract metals from
their ores, his only implements were formed of stone; and before he became
acquainted with iron, there was an intermediate period in which the
more easily obtained metal, copper, had to serve as the material for all
tools and weapons. Hence archæologists speak of the stone age, the
bronze age, and the age of iron. If we were obliged to name the nineteenth
century after the material which distinctively serves in it for the most extensive
and varied uses, surely we should call it the Age of Indian-rubber!
The industrial application of Indian-rubber is entirely modern. The
substance itself appears, however, to have been known to the natives of
Peru from time immemorial, and to have been used for the preparation of
some kind of garments. Although the first specimens were sent to Europe
so long ago as 1736, and the substance was from that time submitted to
725many investigations, no other use was found for it up to the year 1820 than
to efface from paper the marks made by pencils. From this it derives the
name by which it is commonly known. It has also been called “gum elastic,”
and caoutchouc from the Indian name. Crude caoutchouc is the product
obtained by the spontaneous solidifying of the milky juice of certain tropical
plants—such as the Hævea elastica, Jatropha elastica, and the Siphonia
cautshu. The first grows chiefly in South America, and in the basin of the
Amazon forms immense forests. At a certain season each year bands of
persons, called “seringarios,” armed with hatchets, visit these forests for the
purpose of extracting the caoutchouc. They make incisions into the trunk,
and the milky juice immediately runs out, and drops into a vessel placed
to receive it, and attached to the tree by means of a lump of clay. In about
three hours the juice ceases to flow, and the seringario collects the products
of the incisions in one large vessel. By dipping a board into this
vessel, it becomes covered with the juice; and when this is allowed to dry,
the caoutchouc remains as a thin brownish yellow layer. The caoutchouc
is not dissolved in the juice, but is merely suspended in it; and to hasten
the drying and coagulation of the liquid, the board is warmed over a smoky
fire made with green wood. When alternate immersions and drying have
covered the board with a sufficient thickness of caoutchouc, the layer is
slit open with a knife, and the board is withdrawn. This is the best kind
of crude caoutchouc, because it is free from all admixture of foreign bodies
except the carbon derived from the smoky flame. The bottle Indian-rubber
is moulded on pear-shaped lumps of clay, which are covered with
successive layers of the milky juice; when a sufficient thickness has been
attained, the clay is removed by soaking in water.
Up to 1820, as already mentioned, Indian-rubber was used only for
effacing pencil-marks, and about that time a piece half an inch square sold
for two shillings and sixpence. But the extreme elasticity and extensibility
of this singular substance was attracting the attention of practical men in
England, Scotland, and France. One of the earliest patents obtained in
this country for applications of caoutchouc was taken out by Mr. Thomas
Hancock, of Newington, in 1820. This gentleman has written an account
of the Indian-rubber manufacture from the commencement, and the book
is extremely interesting from the clear and simple manner in which the
inventor describes how he effected one improvement after another in his
processes and machinery. Mr. Hancock had, previous to his turning his
attention to Indian-rubber, no acquaintance with chemistry; but he was
skilled in mechanical engineering and the use of tools, and this knowledge
proved to be precisely the kind most valuable for dealing with the first
stages of caoutchouc manufacture. His first patent was for the use of
Indian-rubber for the wrists of gloves, for braces, for garters, for boots and
shoes instead of laces, and for other similar purposes. The rings for the
wrists of gloves, &c., were simply cut from the bottle Indian-rubber by
machinery the patentee himself contrived for that purpose. Mr. Hancock
next arranged an apparatus for flattening the raw Indian-rubber by warmth
and pressure, so as to make it available for the soles of boots, &c. He
relates the practical difficulties he had to encounter in his operations, and
the manner in which he overcame them. He soon noticed and utilized
the fact that two clean freshly-cut surfaces of caoutchouc, when pressed
together, cohere and unite perfectly. This further led him to devising a
machine by which all the waste cuttings and parings might be worked up.
This machine consisted of a cylinder revolving within a cover, both being
726provided with steel teeth, by which the pieces of caoutchouc placed between
them were torn into shreds, and then kneaded into a solid coherent
mass of homogeneous texture. The first machine of this kind made by
Mr. Hancock would work up about 1 lb. of Indian-rubber; but now machines
on the same principle are in use operating on more than 200 lbs. of
material at once, and turning it out on a roll 6 ft. long, and 10 in. or 12 in. in
diameter.
While Hancock was thus successful in mechanically working Indian-rubber,
Macintosh, of Glasgow, found means of effecting its solution by
coal-naphtha, and he obtained, in 1823, a patent for the application of his
discovery to the fabrication of waterproof garments. Waterproof cloth, or
“Macintosh,” is prepared by varnishing one side of a suitable fabric with
a solution of caoutchouc, or by covering one side of a cloth with a thin
film, and then bringing it into contact with a second piece similarly prepared—the
two caoutchouc layers becoming incorporated when the double
cloth is passed between rollers. Other solvents for Indian-rubber have
been discovered in ether, chloroform, sulphide of carbon, and rectified
turpentine. By treatment with these liquids it swells up, and eventually
dissolves, producing a viscid ropy mass, which, by evaporation of the
solvent, leaves the caoutchouc with all its original elasticity. By the use
of these last-named solvents the persistent and disagreeable odour occasioned
by coal-oil is avoided. Mr. Hancock relates that when the manufacturers
had overcome all obstacles, and had succeeded in producing
thin, light, pliable, and perfectly waterproof fabrics, they had to encounter
another quite unexpected difficulty—the tailors set their faces against the
new material, and could not be induced to make it up! The manufacturers
were, therefore, obliged themselves to fashion waterproof garments,
and retail them to the public. This, however, turned out to be a benefit,
for the seams were made waterproof, so as to exclude even the little water
which would otherwise pass in by capillary attraction at the stitches.
It will now be observed that there are two distinct modes of working
caoutchouc: by dealing, viz., with the solid material, or with the solutions.
Thus, from a solid disc of caoutchouc long ribbons of the material may be
cut, and these ribbons, by being passed between a set of circular knives,
may be divided into a number of square threads. These threads may then
be drawn out to six or ten times their length; and, if wound and maintained
in this state of tension for forty-eight hours in a warm place, they
will lose their condition of tension, and their elongated form will become
their natural or unstrained one. In this manner are the Indian-rubber
threads prepared, which, covered with silk or other material, form elastic
fabrics such as those used in the sides of boots. The circumstance of
caoutchouc, when heated for some hours at a temperature a little above
the boiling-point of water, retaining whatever form it has during the heating,
is the basis of methods of obtaining thin sheets and other forms of the
material. Tubes are made by forcing the heated caoutchouc through an
annular opening by application of great pressure; it sets in cooling, preserving
a section corresponding with the orifice through which it issues.
In another mode of forming tubes, a paste composed of caoutchouc, oxide
of zinc, and lime, is formed into sheets, which are cut into strips. The strips
are folded longitudinally, and the edges are cut together at an angle of
45° with the surface, so that the cut surfaces may meet each other when
the strip is rolled on a mandril to give it a cylindrical form. A slight
pressure suffices to solder together the cut surfaces, and the tube is then
“vulcanized” by a process to be presently described.
727The dissolved caoutchouc serves to prepare waterproof garments, round
threads, sheets of Indian-rubber, &c. Fabrics are coated with the solution
by pouring it on the material as it is passing horizontally from a roller. A
straight-edge, under which the charged cloth passes, distributes the caoutchouc
in a uniform layer, the thickness of which is regulated by the space
between the knife-edge and the fabric. When sulphide of carbon is the solvent
used, its evaporation is complete in about ten minutes, but with other
solvents two or three hours are required. The caoutchouc is usually mixed
with lampblack before being spread on the cloth, and the article is finished
by giving the Indian-rubber layer a coat of gum-lac varnish. Sheets of
Indian-rubber are obtained by spreading fifteen or twenty layers over a
cloth, which is afterwards detached by wetting it with a solvent.
Threads of circular section are manufactured from a paste of caoutchouc,
made by dissolving that substance in sulphide of carbon mixed with 8
per cent, of alcohol. This paste is placed in a cylinder, out of which it is
forced by a piston through a number of circular holes, whence it issues in
the form of filaments. These are received upon a stretched cloth, which
moves along, carrying the parallel threads, until the sulphide of carbon
has evaporated.
A modification of caoutchouc, possessing very valuable qualities for many
purposes, was discovered by Mr. Charles Goodyear, and largely applied by
him in the United States to the fabrication of waterproof boots. In 1842
these boots were imported into Europe, and it was seen that this form of
the material had the advantages of not sticking to other bodies at any
ordinary temperatures, and of preserving its elasticity even in the coldest
weather, whereas ordinary Indian-rubber becomes rigid by cold. The cut
edges of this variety of caoutchouc do not cohere by pressure. Mr. Goodyear
attempted to keep his process a secret; but Mr. Hancock, having soon
detected the presence of sulphur in the American preparations, set to work
to discover how that substance was made to combine with the caoutchouc.
He succeeded, and he obtained a patent for sulphurizing Indian-rubber
before the original inventor had applied for one. Mr. Hancock found
that a sheet of caoutchouc immersed in melted sulphur at 250° F., gradually
absorbed from 12 to 15 per cent, of its weight of sulphur; and,
further, that this does not in any way alter its properties. When, however,
the sulphurated substance was for a few minutes exposed to a temperature
of 300°, it acquired new qualities, which were precisely those of the modification
employed by Mr. Goodyear for his impervious boots. This transformation
effected by sulphur Mr. Hancock called vulcanization; and
vulcanized Indian-rubber is now employed in nearly all the innumerable
applications of caoutchouc, provided the presence of sulphur is not absolutely
objectionable. Goodyear’s process consists in mixing the sulphur
with the caoutchouc, the suitable proportion (7 to 10 per cent.) having
been determined beforehand, and the sulphur ground up with the Indian-rubber
in the masticating machine, or disseminated through the viscid liquid
if a solution is used, or dissolved in the solvent employed. This gives better
results than Hancock’s process, because the sulphurization is more uniform,
and this method is therefore more largely employed. When the various
articles have been fabricated in the ordinary manner from the mixture of
caoutchouc and sulphur, they are enclosed in vessels, where they are submitted
for two or three hours to the action of steam under a pressure of
nearly 4 atmospheres, so that the steam may have a temperature of about
280° F. A still easier method, due to Mr. Parkes, consists in steeping the
728articles (which in this case should be thin) in a solution of one part of chloride
of sulphur in sixty of bisulphide of carbon. The object becomes vulcanized
by simple exposure to the air, without the aid of heat. But this process is
said to be liable to cause the article afterwards to become brittle. The
addition of oxide of zinc, carbonate of lead, and other substances, is found
to yield a product better adapted for certain purposes than one in which
only sulphur is used.
The list of applications of vulcanized Indian-rubber would be a very long
one; but as a great number of these applications must be known to everybody,
it will be unnecessary to specify them. It has lately been used for
carriage-springs, for the tires of wheels, and for the rollers of mangles. Its
employment in the construction of portable boats, pontoons, life-buoys,
dresses for divers and for the preservation of life at sea, air-tight bags and
cushions, air and water beds, cushions of billiard-tables, are a few of the
thousand instances of its utility which might be quoted.
When the proportion of sulphur mixed with the caoutchouc is increased
to 25 or 35 per cent., another product having qualities entirely different
from those of vulcanized Indian-rubber is obtained when the mixture is
heated. This is the jet-black substance termed ebonite or vulcanite, which
is made into such articles as combs, paper-knives, buttons, canes, portions
of ornamental furniture, and plates of electrical machines. It is in many
cases an excellent substitute for horn and for whalebone, while for insulating
supports, &c., in electric apparatus, it is unrivalled. It has a full
black colour and takes a bright polish; and it may be cut, or filed, or
moulded. It is very tough, hard, and durable. In the transformation of
Indian-rubber into vulcanite, the temperature must be somewhat higher
than that required for the production of the vulcanized Indian-rubber. The
caoutchouc used is very carefully purified before it is incorporated with the
sulphur; and the yellow paste formed by the mixture is subjected to the
contact of steam at a temperature of about 310°.
Gutta-percha is a substance very like Indian-rubber in its chemical
properties, having the same composition, although in outward appearance
very different. It was first sent to Europe in 1822, but did not become
an article of commerce until 1844. It is the solidified juice of a tree (Isonandra
percha) which abounds in Borneo and Malacca. The trunk of the
tree grows to a diameter of 6 ft., but as timber it is valueless. When an incision
is made through the bark and into the wood, a milky juice flows out,
which speedily solidifies. Gutta-percha is a very tough substance, but is
without the elasticity of Indian-rubber. It differs from the latter, too, in
becoming softened by a gentle heat, and it will then readily take and
retain any impressions with great sharpness and fidelity. Thus beautiful
mouldings and other ornamental objects are easily made. It also has the
valuable quality of welding when softened by heat. It is a non-conductor
of electricity, and it is largely used for covering telegraph-wires, and especially
for forming an insulating coating in submarine cables. It seems to
have become known precisely at the time it was required for this purpose,
729and the success of ocean telegraphy is largely owing to its valuable properties.
It is employed as a substitute for leather in soling shoes and boots,
and in forming straps and bands for driving machinery; also in the preparation
of tubes used for conveying liquids, and for speaking-tubes. Dilute
mineral acids have no action upon it, and hence it is especially valuable for
making bottles to contain hydrofluoric acid, which attacks glass. A drawback
to the use of gutta-percha is its tendency to become oxidized when
exposed to light and air, by which it entirely loses its power of becoming
plastic by heat, and is converted into a brittle substance. But in the dark,
or under water, it may, however, be preserved for an indefinite period
without change.
Mr. Charles Hancock, in 1847, patented a machine for cutting the gutta-percha
into slices. In this machine there is a circular iron plate, with three
radial slots, in which knives are fixed somewhat in the manner of the cutting
tool of a spokeshave. The lumps of gutta-percha drop against these
knives as the plate is driven round, and the material is cut into slices, which
have a thickness determined by the projection which has been given to the
blades. Sometimes an upright chopper is used, with straight or curved
blades. These slices are immersed in hot water, until they are softened,
and they are then subjected to the action of rollers armed with toothed
blades, called “breakers,” and also to the action of the mincing cylinder,
which is furnished with radiating blades, and revolves partly immersed in
the water. The material is carried out of the hot water to these machines
by endless webs mounted on rollers. The breakers and mincing cylinders
make about 800 revolutions per minute. The gutta-percha, thus reduced
to fragments, is carried forward again by endless webs into cold water, where
it is thoroughly washed and separated from the impurities, which fall to the
bottom, while the lighter gutta-percha floats on the surface of the water.
Gutta-percha, like caoutchouc, can be combined with sulphur. The
best product is obtained when a small proportion of sulphur is used along
with some metallic sulphide. Mr. C. Hancock uses 48 parts of gutta-percha,
1 of sulphur, and 6 of antimony sulphide. These ingredients are
thoroughly mixed and put into a boiler, where they are heated under pressure
for an hour or two. Another method of treating gutta-percha was also
devised by Mr. C. Hancock, who found that when this strange substance
was exposed to nitric oxide gas (which is given off when nitric acid acts
on copper) it became quite smooth, and acquired an almost metallic lustre,
losing also all its stickiness. Another modification is formed by treating
gutta-percha with chloride of zinc; and yet another by the action of a solvent,
such as turpentine, a sulphide, sulphur, and carbonate of ammonia,
employed simultaneously. Mr. Hancock mixes all these materials together
in a “masticator,” and then applies heat to them while confined in a vessel
under pressure. The product of these operations is a very singular modification
of gutta-percha, in which the material assumes a spongy, elastic condition,
and in this form it is used to form the stuffing of sofas, easy chairs,
&c. Among the purposes to which gutta-percha has been applied besides
the general one of waterproof tissues and fabrics, may be named the formation
of straps, belts, bandages, cups, and other vessels, rollers for cotton-spinning
machinery, hammers of pianofortes, cards for wool-carding,
hammercloths, life-preservers, and trusses.
Gutta-percha is made into strips, bands, cords, or threads of any required
section, by passing sheets of suitable thickness between rollers provided
with grooves and cutting edges. For strips and bands the sheets are passed
730through the machine cold, and divided by the cutting-edges. But for round
cords or threads sheets are supplied to the rollers from a receptacle in which
they acquire a temperature of about 200° F. The material is forced to take
the form of the grooves, the operation in this case being analogous to that
of rolling iron bars. The gutta-percha cords are received as they issue
from the rollers in a tank of cold water, from which they pass on, to be
wound on reels or drums. It is obvious that cords of any section may be
formed by making use of grooves of suitable shape. Tubes of gutta-percha
are made by forcing the softened substance out of an annular orifice:
it is received into vessels filled with cold water. Telegraph-wires
are covered by a similar process—the copper wire being made to pass
through the centre of a circular opening with the gutta-percha surrounding
it. Picture-frames, &c., are made by forcibly pressing warm gutta-percha
into the warmed moulds. Gutta-percha tubing is largely used
everywhere for the speaking-tubes by which persons in remote apartments
of even the largest building can converse. This is one of the labour-saving
inventions of our day. It must have struck every one who has seen
these speaking-tubes in operation in a large establishment, what a vast
amount of running to and fro they save, and how much they expedite
business by the convenient means they afford of giving orders and directions
to persons in distant apartments. This tubing is also used for the
conveyance of liquids, and it has been proposed to employ it instead of the
ordinary leaden piping used for carrying water. It may seem to the reader
that gutta-percha is too fragile a material to resist the pressure to which
water-pipes are exposed. But, judging from some experiments made by
the engineer of the Birmingham Waterworks, the power of gutta-percha
tubing to resist pressure is quite extraordinary, and far beyond what would
be supposed. The tubes experimented on had diameters of ¾ and ⅞th of
an inch respectively. The water from the main, where the pressure was
that caused by a head of 200ft., was in communication with these pipes for
several weeks, and they were found unaltered in any way. In order to test
the strength of the tubes, and find the greatest pressure they would bear,
the engineer then had them connected with a hydraulic proving-pump;
and here, when exposed to the highest pressure at which the ordinary
water-pipes were tested, namely, to 250 lbs. on the square inch, they also
remained intact. The pressure was afterwards increased to 337 lbs., but
without any damage to the tubes.
The increasing importance of gutta-percha may be inferred from the continually
augmented importation of the crude substance into this country.
In 1850 only 11,000 cwt. were imported, but the quantity has increased
year by year; and in 1872 we received nearly 46,000 cwt. The demand
is still increasing; but there is reason to apprehend that under the stimulus
of a rising market, the producers have collected the gutta-percha wastefully
and with great destruction of the trees, so that it is not improbable that if
the demand still increases, there may be a gutta-percha famine. The
concreted juices of certain other trees have been proposed as substitutes
for gutta-percha. None of these have as yet come into practical use. The
increase in a few years of the quantity of Indian-rubber imported into the
United Kingdom is perhaps more extraordinary. From the tables given
in Mr. Hancock’s book, it appears that our imports of caoutchouc were
853,000 lbs. in 1850, but by 1855 they had amounted to 5,000,000 lbs.
731
Fig. 338.—Portrait of Sir James Young Simpson, M.D.
ANÆSTHETICS.
The discovery which is indicated by the somewhat unfamiliar word[16]
which heads this article is perhaps the greatest which has ever been
made in connection with the science of medicine. At least, there is no
other discovery of modern times which has so largely and directly contributed
to the assuagement of human suffering. Nay, in this respect there
is perhaps in the whole annals of the healing art no other which can rival
it, if we except that famous one of Jenner’s which has arrested the ravages
of small-pox. During the last thirty years, all the more formidable operations
of the surgeon have been, in almost every case, performed with a happy
unconsciousness on the part of the patient. In unconsciousness, induced
by the same means, has relief also been found for severe suffering arising
from other causes. The substances which are denoted by the word “anæsthetics”
differ from the drugs which the older surgeons sometimes administered
before an operation, in order to lull the patient’s sense of pain.
They differ in their nature and in the mode of their administration; by
the certainty and completeness of their action; by the entirely transient
effects they produce, which pass off without leaving a trace.
16. From α (αν), privative, and αισθητικος, capable of perceiving or feeling.
To the great chemist whose name has already been mentioned as the
732discoverer of the metals of the alkalies and alkaline earths we are indebted
for the first of the remarkable class of bodies we are about to discuss.
The first work that Davy published had for its title “Researches,
Chemical and Philosophical, chiefly concerning Nitrous Oxide and its
Respiration.” This was in the year 1800, when the philosopher had hardly
completed his twenty-first year. The work caused no little sensation in
the scientific world, and it was in consequence of the reputation he acquired
by these researches that Davy was appointed to the chemical professorship
at the Royal Institution. Davy was not the original discoverer of nitrous
oxide, but he first entered upon a full investigation of its properties, and
announced the singular effect produced by its inhalation. The kind of
transient intoxication and propensity to laughter which it excites have obtained
for this compound the familiar name of laughing gas. Davy had
by experiment on his own person proved the anæsthetic properties of this
gas, for he had a tooth painlessly extracted when under its influence,
and he says in the work above named that “as nitrous acid gas seems
capable of destroying pain, it could probably be used with advantage in surgical
operations where there is no effusion of blood.” Davy’s observations
and suggestions were destined to lie barren for nearly half a century, but
they nevertheless formed the basis of the great results which have since
been attained.
Before proceeding farther, it will perhaps be well to make the unscientific
reader acquainted with the chemistry of nitrous oxide. We may presume
that he knows that atmospheric air is a mixture of the two invisible gases,
nitrogen and oxygen (the small quantity of carbonic acid also present need
not now be considered). When a known quantity of air is passed over red-hot
copper turnings, contained in a tube, the whole of the oxygen is seized
upon by the copper, and only the nitrogen issues from the tube, and may
be collected. Some of the copper is thus converted into oxide, and the
increase of the weight of the tube’s contents shows the weight of oxygen
contained in the air, while the weight of nitrogen may be known from the
volume collected. In this way the chemist analyses atmospheric air, and
determines that 100 parts by weight of dry air contain about 79 of nitrogen
and 21 of oxygen; or, by measure, about four times as much of the former
as of the latter. Now, chemists are acquainted with no fewer than five
different substances which contain nothing but nitrogen and oxygen. These
substances are either gases, or can be changed into the gaseous form by
heat, and they can all be analysed in the same manner as air. The results
of such analyses show in 100 parts by weight of each substance the following
proportions of its constituents:
No. 1.
No. 2.
No. 3.
No. 4.
No. 5.
Nitrogen
63·64
46·67
36·84
30·44
25·93
Oxygen
36·36
53·33
63·16
69·56
74·07
In casting the eye over this table, no relation will probably be detected
between the five cases. But if we write down, not the quantities of nitrogen
and oxygen contained in 100 parts of each compound, but the quantity
of oxygen which in each compound is united to some fixed quantity
of nitrogen, we shall at once detect a remarkable law: thus, taking 28 as
the fixed weight of nitrogen, for reasons which need not be here explained:
733
No. 1.
No. 2.
No. 3.
No. 4.
No. 5.
Nitrogen
28
28
28
28
28
{Oxygen
16
32
48
64
80
{ or
16 × 1
16 × 2
16 × 3
16 × 4
16 × 5
Chemists have a sort of shorthand method of expressing the composition
of substances, which may be conveniently illustrated by the case before us.
Let it be agreed that the letter N shall not only represent nitrogen, but
always fourteen parts by weight—grains, ounces, &c., &c.,—of nitrogen;
and that, similarly, O shall stand for sixteen parts by weight of oxygen. It
is plain that the composition of the compound No. 2 may be represented
by simply writing down “NO;” and that of No. 4, in which there is just
double the proportion of oxygen, by “NOO.” But to avoid an unnecessary
repetition of the same symbol, when it has to be taken more than once, a
small figure is written after and a little below it. Thus, for OO, “O2” is
written. The proportional composition of each of the five compounds will
now be obvious from the following symbols:
No. 1.
No. 2.
No. 3.
No. 4.
No. 5.
N2O
NO
N2O3
NO2
N2O5
These symbols may be regarded as merely a compendious expression of
the composition of each substance—as a shorthand statement of the facts
of analysis. But to the majority of chemists the symbols have a deeper
significance; for they are taken as representing the atoms of each element
which enter into each smallest possible particle of a compound; they express
a certain theory of the ultimate constitution of matter. Thus, if we
suppose that there exist indivisible particles of nitrogen and of oxygen,
and that each smallest particle, or molecule, of the compounds under
consideration is constituted of a certain definite and invariable number of
each kind of atoms; and, further, if we suppose that an atom of oxygen is
heavier than one of nitrogen in the proportion of 16 to 14, or 8 to 7, we
shall have a simple theoretical explanation of the relations in the proportions
already pointed out. In fact, these would result from the simplest
combinations of the two kinds of atoms; and we can picture each one of
the smallest particles of the several bodies as thus constituted:
No. 1.
No. 2.
No. 3.
No. 4.
No. 5.
● ● ○
● ○
● ● ○ ○ ○
● ○ ○
● ● ○ ○ ○ ○ ○
N2O
NO
N2O3
NO2
N2O5
The black circles represent nitrogen atoms, and the open ones oxygen
734atoms; the symbols are placed below in order that their relation to the
supposed atomic constitution may be obvious at a glance. While the
symbol of a compound must always accord with its percentage composition,
the latter does of itself determine the symbol or formula. A number
of other circumstances, which cannot here be discussed, are taken into
account as evidence of the constitution of the molecule.
This digression on chemical formulæ will, it is hoped, enable the general
reader, who may not previously have been acquainted with them, to perceive
their significance, instead of passing them over as unintelligible
cabalistic letters when they occur in the following pages. With this object,
it may be added that the elements, hydrogen, carbon, and chlorine,
are respectively represented by H, C, and Cl; and that the proportional
quantities, which are also implied in the symbols, and are those by which
H, C, and Cl combine with other bodies, are 1, 12, and 35·5 respectively.
Another point which should be understood is that the properties and behaviour
of a chemical compound are different, and usually extremely different,
from those of any of its constituents. This is well illustrated in the
subject we are considering. Atmospheric air is a mixture (not a compound)
of nitrogen and oxygen gases, and all its properties are intermediate between
those of its ingredients taken separately. Nitrous oxide, N2O, has
properties not possessed by either constituent separately. For example, it
is very soluble in water, whereas oxygen is very slightly so, and nitrogen
still less. The other compounds we have referred to differ widely from
nitrous oxide and from each other in their properties.
Nitrous oxide is an invisible gas, having a slightly sweetish taste and
smell. It is dissolved by water, which, at ordinary temperatures, takes up
about three-fourths of its volume of the gas. By cold and great pressure
the gas may be condensed into a colourless liquid. The gas is obtained
in a pure state by gently heating the salt called ammonium nitrate, which
is formed by neutralizing pure nitric acid with carbonate of ammonia. The
action which occurs may be explained thus: the hydrogen of the ammonium
unites with a portion of the oxygen of the nitric acid, forming water,
whilst the remainder of the oxygen combines with the nitrogen. As chemical
actions are regarded as either separations or unions of atoms, they
can be expressed by what is called a chemical equation, the left-hand side of
which shows the arrangement of the atoms before the action, and the
right-hand side the arrangement after it, the sign of equality being read as
“produce” or “produces.” But the validity of the equations, like that of
the symbolic formulæ, is quite independent of the existence of atoms; for
the equation always rests on certain facts, namely, the relations between
the quantities of the substances which enter into, and those which are produced
by, a chemical action. Thus, in the present case the action may be
symbolically expressed as follows:
H4N NO3
=
2H2O
+
N2O
Ammonium nitrate.
Water.
Nitrous oxide.
The equation expresses the fact that every 80 parts by weight of ammonium
nitrate, which are used in this reaction, split up into 36 of water and 44 of
nitrous oxide.
No attempt seems to have been made to turn Davy’s suggestion to practical
account; but in courses of chemical lectures at the hospitals and elsewhere
the peculiar physiological properties of nitrous oxide have, since
Davy’s announcement, always been demonstrated by some person inhaling
735the gas. In the medical schools the students often operated on a comrade
who was under the influence of nitrous oxide to the extent of bestowing
sundry pinches and cuffs, which fully proved the anæsthetic qualities of
the nitrous oxide. In 1818 Faraday pointed out the similarity between the
effects of ether and of nitrous oxide, and from that time Professor Turner
regularly included among the experiments of his course of chemistry the
inhalation of the vapour of ether by one of the students. This was done
by simply pouring a little ether into a bladder of air, and by means of a
tube drawing the mixed air and vapour into the mouth. Until 1844 the
effects of nitrous oxide and of ether vapour remained without application,
although thus continually demonstrated in lectures. At the close of that
year, Mr. Horace Wells, a dentist, of Hartford, Connecticut, U.S.A., witnessed
the usual experiments with nitrous oxide at a public lecture. At his
request the lecturer attended at Mr. Wells’s residence the following day, to
administer to him the nitrous oxide, in order that he might try its efficacy
in annulling pain, for he was himself to have a tooth extracted by a brother
dentist. His exclamation on finding the operation painlessly over was,
“A new era in tooth-pulling!” Mr. Wells continued his experiments on the
use of nitrous oxide in dental operations, but he did not apparently obtain
uniform results, for he pronounced its effects uncertain, and he gave it up.
On the occasion when Mr. Wells’s tooth was extracted, Dr. W. T. G. Morton
was present, and he soon afterwards found that under the influence of
ether vapour, teeth might be painlessly extracted and surgical operations
performed. Dr. Morton attempted to conceal the substance he used under
the name of “letheon,” for which he obtained a patent. But the well-known
and characteristic odour of ether declared the nature of the “letheon;” and
Dr. Bigelow having in consequence tried ether, found it to produce all the
effects of “letheon.” So the matter was no longer a secret. Dr. Morton
was, therefore, the person who first applied ether vapour, and the extraction
of a tooth was the occasion of its first application. This was in 1846.
It was used for the first time in England on the 19th of December, 1846,
also for the extraction of a tooth; and two days afterwards Mr. Liston, the
eminent surgeon, performed the operation of amputating the thigh while
his patient was under the influence of ether. The employment of ether
in surgical operations quickly spread, and its administration in hospitals
became general throughout Europe and America.
The chemical constitution of ether, and its relation to alcohol, may be
indicated by the following formulæ:
HOH
HO(C2H5)
(C2H5)O(C2H5)
Water.
Alcohol.
Ether.
If we suppose one of the hydrogen atoms in the molecule of water to
be removed and replaced by the group (C2H5), the result is alcohol. If,
now, (C2H5) be substituted in the alcohol for the remaining atom of hydrogen,
we get a particle of ether. Ether was discovered in 1540, and described
as sweet oil of vitriol, but its real nature was first pointed out by
Liebig. It is prepared by distilling a mixture of sulphuric acid and alcohol.
It is a colourless transparent liquid, extremely volatile, and possessing a
peculiar and powerful odour. It evaporates so rapidly that a drop allowed
to fall from a bottle on a warm day may be converted into vapour before
it reaches the ground. When its vapour is inhaled in sufficient proportion
mixed with air, it soon produces a complete insensibility to pain. In the
case of a full-grown man who inhales air containing 45 per cent. of the
736vapour, about 2 drams per minute of the liquid are consumed. The air is
allowed to stream over the surface of the liquid in a proper apparatus,
where it takes up the vapour, and the two pass through a flexible tube to a
piece fitting over the mouth and nostrils of the patient. The effects produced
are progressive, and may be thus described:
For about two minutes after the beginning of the inhalation, the patient
retains his mental faculties, and has some power of controlling his movements,
but in a confused and disordered manner. At the end of the third
minute he is unconscious; there are no voluntary movements, but muscular
contractions may agitate the frame. At the end of the fourth minute, the
only perceptible movements are the motions of the chest in respiration. If
the inhalation be discontinued at the end of the fourth minute, when 1 oz.
of ether will have evaporated, similar stages are passed through in reverse
order during recovery. The condition reached at the end of the fourth
minute continues about two minutes; the intermediate state lasts three
or four minutes; the condition of confused intellect and will about five
minutes. This is succeeded by a feeling of intoxication and exhilaration,
which continues for ten or fifteen minutes. It was probably this excitement
of the system produced by ether which has caused it to be superseded—in
Britain, at least—in about twelve months after its adoption, by
chloroform.
Chloroform appears to have been independently discovered in 1831, by
Soubeiran, and by an American chemist, Guthrie. It is usually procured by
distilling a mixture of bleaching powder, spirits of wine, and water. Chloroform
is a colourless volatile liquid, of an odour much more agreeable than
that of ether. Its composition is represented by CHCl3. The merit of
having first applied the singular properties of this substance to the alleviation
of human suffering belongs to the late Sir J. Y. Simpson, of Edinburgh.
Its use as an anæsthetic was apparently suggested to this eminent professor
by Mr. Waldie, of Liverpool. It was first applied at Edinburgh on the
15th November, 1847; and when its efficacy had been proved, it was soon
extensively used, and in Europe, at least, almost entirely superseded ether,
as being more rapid and certain in its action, not producing injurious excitement,
and being pleasanter to inhale. A notion prevailed that chloroform
was not only more powerful in its operation than ether, but also more
safe. In January, 1848, its administration, however, proved fatal to a patient;
and since then a certain number of casualties of this kind have occurred
with chloroform, ether, and other anæsthetics.
The patient is often made to inhale the vapour of chloroform by merely
holding before his mouth and nostrils a sponge or handkerchief, on which
a small quantity of the liquid has been poured. Dr. Snow contrived an
apparatus for administering the vapour with more regularity. A metal box
adapted to the shape of the face is made to cover the mouth and nostrils.
This piece has two valves, one of which admits the air and vapour from an
elastic tube connected with the apparatus containing the chloroform, and
prevents its return; the other valve is a flap opening outwards, which
allows the expired air to escape. There is also an adjustment for admitting
directly into the mouthpiece more or less atmospheric air.
The sensations first experienced when chloroform is inhaled are said to
be agreeable. Many persons have described the feeling as resembling rapid
travelling in a railway carriage; there is a singing in the ears, and when
the power of vision ceases, and the person is no longer conscious of light,
the sensation is that of entering a tunnel. After this there is a lessened
737sensibility to pain; and in the next stage the unconsciousness to outward
impressions is deeper, but the mental faculties, though impaired, are not
wholly suspended, for the patient may speak, and usually dreams something
which he afterwards remembers. When the person is still more
under the influence of the chloroform, no voluntary motions take place,
although there may be some inarticulate muttering. Dr. Snow describes
several conditions which may be observed in patients undergoing operations
under the influence of chloroform. First, the patient may preserve
the most perfect quietude without a sign of consciousness or sensation;
this is the most usual condition. Second, he may moan, or cry, or flinch
under the operation, without, however, having the least memory of any pain
when he recovers. Third, the patient may talk, laugh, or sing during the
operation; but what he says is altogether devoid of reference to what is
done. Fourth, he may be conscious of what is taking place, and may look
on while some minor operation is proceeding, without feeling it, or without
feeling it painfully. This is often the condition of the patient as the
effect is passing off, while some smaller operation is still proceeding. Fifth,
the patient may complain he is being hurt; but afterwards, when the effect
of the chloroform has passed off, he will assert that he felt no pain whatever.
When the chloroform has been inhaled for but a short time, the
patient becomes conscious in about five minutes after its discontinuance;
but with a longer inhalation the period of unconsciousness may last for
perhaps ten minutes. The return of consciousness takes place with tranquillity:
not unfrequently the patient’s first speech, even after a serious
operation, often being an assertion that the chloroform has not taken
effect.
In the strongest degree of ether and chloroform effects, all the muscles
of the body are relaxed; the limbs hang down, or rest in any position in
which they are placed; the eyelids droop over the eyes, or remain as they
are placed by the finger; the breathing is deep, regular, and automatic;
there is often snoring, and this is, indeed, characteristic of the deepest
degree of unconsciousness; the relaxation of the muscles renders the face
devoid of expression, and with a placid appearance, as if the person were
in a sound natural sleep. He is perfectly passive under every kind of operation.
The breathing and the action of the heart proceed all the while with
unimpaired regularity. It is, however, known by experiments on animals
that if the inhalation be prolonged beyond the period necessary to produce
these effects, the respiratory functions are interfered with by the insensibility
extending to the nerves on which they depend. The breathing of an
animal thus treated becomes irregular, feeble, or laborious, and death ensues.
However nearly dead from inhalation of ether vapour the animal
may be, provided respiration has not actually ceased, it always recovers
when allowed to breathe fresh air. Of course, the etherization is never
carried to this stage with human beings.
Air containing 2 grs. of chloroform in 100 cubic inches suffices to induce
insensibility; but 5 grs. in 100 cubic inches is found a more suitable proportion.
Dr. Snow, who strongly disapproved of the uncertain and irregular
mode of administering chloroform on a handkerchief or sponge,
contrived the inhaling apparatus already described. The air before reaching
the mouth and nostrils of the patient passes through a vessel containing
bibulous paper moistened with chloroform. This vessel he surrounds with
water at the ordinary temperature of the air, in order to supply the heat
absorbed by the conversion of the liquid into vapour, so that the formation
738of the latter may go on regularly. The same thoughtful arrangement
formed part of the ether-inhaler he had previously contrived.
The extraordinary effects of ether and chloroform have introduced new
and important facts into psychological science, and have illustrated and
extended some of the most interesting results of physiological research.
Let us trace the action of these substances, and explain it as far as may
be. Nitrous oxide, ether vapour, and chloroform vapour are all soluble in
watery fluids. The lungs present a vast surface bathed by watery fluids,
and therefore these gases are largely absorbed; and by a well-known process,
they pass directly into the blood, through the delicate walls of the
capillary vessels. The odour of ether can be detected in any blood drawn
from persons under its influence. Ether, or chloroform, thus brought into
the general current of the circulation, is quickly carried to all parts of the
body, and thus reaches the nerve-centres. On these it produces characteristic
effects by suspending or paralysing nervous action: why or how this
effect takes place is unknown. The nervous centres are not all acted upon in
an equal degree—some require a larger quantity of the drug to affect them at
all. The parts of the nervous system first affected are the cerebral lobes,
which are known to be the seat of the intellectual powers. The cerebellum—the
function of which there is reason to believe is the regulation and coordination
of movements—is the next to yield to the influence. Then follow
the spinal nerves, which are the seat of sensibility and motive power. This
is as far as the action can safely be carried: the nervous centre called the
medulla oblongata, which is placed at the junction of the brain and the
spinal cord, still performs its functions—one of the most important of which
is to produce the muscular contractions that keep the respiratory organs
in action. We have seen, by the effects of further etherization in animals,
that when this part of the system is affected, the animal dies from a stoppage
of the respiration.
But, unfortunately, there have been instances in which death has been
caused by the administration of ether and chloroform even under the most
skilful management. But these occurrences were not the result of the inhalation
having been carried so far as to stop respiration: in some cases the
patient has died before the first stage of insensibility. These fatal cases have
all been marked by a sudden paralysis of the heart—that organ has abruptly
ceased to act. Why in these, certainly a very small percentage of patients,
the action of the drug should at once take effect on the heart has not yet
been explained. The rhythmic action of the heart depends upon nervous
centres enclosed within its own substance, so that this organ is to a certain
extent independent; but it is connected with the other nervous centres by
the branches of a remarkable nerve which proceeds from the medulla oblongata,
and also by another set of nerves which come from the chain of
ganglia called the sympathetic nerve. The nerve connecting the heart with
the medulla is a branch of that called the pneumo-gastric, and it is a well-established
fact that the action of the heart may be arrested by irritation
of this nerve. The comparatively few fatalities which have attended the
use of anæsthetics may, therefore, be due either to an immediate action on
the nerve-centres of the heart, or possibly to a mediate action through the
medulla and the pneumo-gastric nerve.
Soon after the introduction of ether the use of nitrous oxide was discontinued
by the dentists, on account of the apparent uncertainty of its action.
Within the last few years, however, its employment in the extraction of
teeth has been revived by Dr. Evans, of Paris, who found that to insure
739certainty in its action, the great point is the inhalation of the gas in a pure
state and without admixture of air. Nitrous oxide seems now to be extensively
used by dentists, and thus Davy’s experiment of 1800 is repeated
and verified daily in thousands of cases, and to the great relief of hundreds
who probably never heard his name.
Other bodies, such as amylene (C5H10), carbon tetrachloride (CCl4), &c.,
have been tried as substitutes for ether and chloroform; but having been
found less efficacious or more dangerous, their use has been abandoned.
It might be instructive to reflect how much unnecessary pain would have
been spared to mankind had ether and chloroform been known and applied
at an earlier age. We know not what other beneficent gifts chemistry
may yet have in store for the alleviation of suffering, but it is unlikely that
even ether and chloroform are her derniers mots. It should be remembered
that the chemists who discovered and examined these bodies were attracted
to the work by nothing but the love of their science. They had no idea
how invaluable these substances would afterwards prove. The chemist of
the present day, whose labour is often its own reward, may be cheered and
stimulated in his toil by the thought that while no discovery is ever lost,
but goes to fill its appropriate place in the great edifice of science, even
the most apparently insignificant truth may directly lead to invaluable results
for humanity at large.
What strange things the ancient thaumaturgists might have done had
they been possessed of the secret of chloroform or of nitrous oxide! What
miracles they would have wrought—what dogmas they would have sanctioned
by its aid! But the remarkable effects produced by the inhalation
of certain gases or vapours were not altogether unknown to the ancients—although
these effects were then attributed to anything but their real
cause. It is related that a number of goats feeding on Mount Parnassus
came near a place where there was a deep fissure in the earth, and thereupon
began to caper and frisk about in the most extraordinary manner.
The goatherd observing this, was tempted to look down into the hole, to
see what could have caused so extraordinary an effect. He was himself
immediately seized with a fit of delirium, and uttered wild and extravagant
words, which were supposed to be prophecies. The knowledge of the presumed
divine inspiration spread abroad, and at length a temple in honour
of Apollo was erected on the spot. Such was the origin of the famous
Oracle of Delphi, where the Pythoness, the priestess of Apollo, seated on
a tripod placed over the mysterious opening, delivered the response of the
god to such as came to consult the oracle. It is stated by the ancient
writers, that when she had inhaled the vapour, her eyes sparkled, convulsive
shudders ran through her frame, and then she uttered with loud cries
the words of the oracle, while the priests who attended took down her incoherent
expressions, and set them in order. These possessions by the
spirit of divination were sometimes violent. Plutarch mentions a priestess
whose frenzy was so furious, that the priests and the inquirers alike fled
terrified from the temple; and the fit was so protracted that the unfortunate
priestess herself died a few days afterwards.
740
Fig. 339.—A Railway Cutting.
EXPLOSIVES.
The illustration above will serve to remind the reader of the great importance
of explosive agents in the operations of civil industry. By
reason of the more impressive and exciting spectacles which attend the
use of such agents in warfare, we are rather apt to lose sight of their far
more extensive utility as the giant forces whose aid man invokes when he
wishes to rend the rock in order to make a road for his steam horse, or in
order to penetrate into the bowels of the earth in search of the precious
ore. A little reflection will show that if such work had to be done with
only the pickaxe, the chisel, and the crowbar, the progress would be painfully
slow; and railway cuttings through masses of compact limestone,
like that represented in Fig. 339, for example, would be well-nigh impossible.
The formation of cuttings and tunnels, and the removal of rocks in
mining operations, are not the only service which explosive agents render
to the industrial arts; there is, besides other uses which might be enumerated,
the preparation of foundations for buildings, bridges, harbours, and
lighthouses. The use of gunpowder in all such operations as those which
have been referred to is too well known to require description. But of late
years gunpowder has been to a great extent superseded for such purposes
by two remarkable products of modern chemistry, called gun-cotton and
nitro-glycerine. Military art has also benefited by at least one of these
741products; and the use of charges of gun-cotton for torpedoes has already
been described and illustrated in these pages.
It is not a little curious that the two most terribly powerful explosives
known to science should be prepared from two most harmless and familiar
substances. The nice, soft, clean, gentle cotton-wool, in which ladies wrap
their most delicate trinkets, becomes, by a simple chemical transformation,
a tremendously powerful explosive; and the clear, sweet, bland liquid,
glycerine, which they value as a cosmetic for its emollient properties, becomes,
by a like transformation, a still more terrifically powerful explosive
than the former. It is, perhaps, even more curious that having undergone
the transformation which confers upon it these formidable qualities, neither
cotton-wool nor glycerine is changed in appearance. The former remains
white and fleecy; the latter is still a colourless syrupy-looking liquid.
The fibres which form cotton, linen, paper, and wood, are composed almost
entirely of a substance which is known to the chemist as cellulose or cellulin.
That this substance, as it exists in the fibres of linen and in sawdust,
could be converted into an explosive body by the action of nitric acid, appears
to have been first observed by the French chemist, Pelouze, in 1838.
The action with cellulose in the form of cotton-wool was more fully examined
by Professor Schönbein, of Basle, who, in 1846, first described the method
of preparing gun-cotton, and suggested some uses for it. He directs that
one part of finely-carded cotton-wool should be immersed in fifteen parts of
a mixture of equal measures of strong sulphuric and nitric acids; that after
the cotton has remained in the mixture for a few minutes, it should be removed,
plunged in cold water, and washed until every trace of acid has
been removed, and then carefully dried at a temperature not exceeding the
boiling-point of water.
After Professor Schönbein had demonstrated the power of the new agent
in blasting, and its projectile force in fire-arms, its manufacture on a large
scale was undertaken at several places. Messrs. Hall commenced to make
it at their gunpowder works at Faversham, and a manufactory was also
established near Paris. In July, 1847, a fearful explosion of gun-cotton
occurred at the Faversham works, which was believed to have been
caused by the spontaneous detonation of that substance. This induced
Messrs. Hall to discontinue the manufacture as too dangerous; and they
even destroyed a large quantity of the product which they had in hand by
burying it in the ground. The making of gun-cotton was soon afterwards
discontinued also by the French, who did not find the substance to possess
all the qualities fitting it for military use. The Prussian Government also
began to make gun-cotton; but the experiments were put a stop to by the
explosion of their factory. An eminent artillery officer in the Austrian
service, General von Lenk, undertook a thorough examination of the manufacture
and properties of gun-cotton for military purposes. He introduced
several improvements into the processes of the manufacture; and the
Austrian Government established works at Hïrtenberg, with a view to the
adoption of gun-cotton as a substitute for gunpowder in fire-arms. It has
some undoubted advantages over powder, for it neither heats the gun nor
fouls it, and it produces no smoke. Notwithstanding this the Austrians
have not abandoned the use of gunpowder in favour of gun-cotton.
Gun-cotton, as a military agent, has a strenuous advocate in Professor
Abel, who presides over the Chemical Department of the British War
Office. To this gentleman we are indebted for great improvements in the
manufacture of gun-cotton, and for a more complete investigation of its
742properties. Professor Abel’s processes were put in practice at a manufactory
which the Government established at Waltham Abbey; and Messrs.
Prentice also set up works at Stowmarket.
Some details of the mode in which the manufacture of gun-cotton was
carried on at Stowmarket may be of interest. The cotton was first thoroughly
cleansed and carefully dried; and these operations are of great
importance, for unless they are well performed, the product is liable to
explode spontaneously. The cotton was then weighed out in charges of
1 lb., and each charge was completely immersed in a separate vessel, containing
a cold mixture of sulphuric and nitric acids. After a short immersion
the cotton was removed from the liquid, and with about ten times its
own weight of acids adhering to it, each charge was placed in a separate
jar, where it was allowed to remain for forty-eight hours. The vessels were
kept cool during the whole period by being placed in a trough through
which cold water was flowing. On removal from the jars, the cotton was
freed from adhering acid by being placed in a centrifugal drying machine.
It was then drenched with a large quantity of cold water, and dried, washed
again in a stream of cold water for forty-eight hours, and the operations
of alternately washing for forty-eight hours and drying were repeated eight
times. The drying was effected by placing the material in cylinders of
wire-gauze, which were whirled round by a steam engine at the rate of 800
revolutions per minute, so that the water was expelled by centrifugal force.
The cotton was next reduced to a pulp by a process similar to that which
is employed in paper-making, and the moist pulp was rammed into metallic
cylinders by hydraulic pressure, in order that it might be brought into
forms suitable for use in blasting, &c. The pulp was put into these moulds
while wet, but the water was nearly all expelled by the compression. The
cylinders of gun-cotton thus obtained were then covered with paper-parchment,
and finally dried at a steam temperature, with many precautions.
The compression of the cotton pulp, by bringing a large quantity of the
material into a smaller bulk, causes a greater concentration of the explosive
energy, and this is a matter of great importance in blasting.
We may now consider what chemistry has to teach concerning the nature
of the action by which cotton-wool is converted into gun-cotton. Cotton
itself is nearly pure cellulose. The chemical composition of cellulose may
be represented most simply by the formula C6H10O5. Nitric acid is a
powerful oxidizing agent, and is constantly used in chemistry to fix oxygen
in various substances; but another kind of action exerted by nitric acid in
certain cases consists in the substitution of a portion of its atoms for hydrogen,
by which the residue of the particle of nitric acid is converted
into water. The formula for nitric acid may be written HO NO2, and it
will be seen that by changing NO2 for H, water, HOH, would be produced.
This is precisely the kind of action which occurs when cellulose
is converted into nitro-cellulose. Two or three, or more, atoms of hydrogen
may be taken out of cellulose, and replaced by two or three, or more, groups
NO2, and the result will be a different kind of nitro-cellulose, according to
the number of atoms in the molecule replaced by NO2. Several varieties
of gun-cotton are known, these being doubtless the result of the differences
here alluded to. The action producing di-nitro-cellulose is represented by
this equation:
C6H10O5
+
2HNO3
=
C6H8(NO2)2O5
+
2H2O.
Cellulose.
Nitric acid.
Di-nitro-cellulose.
Water.
743The equation shows that water is produced by the reaction, and the sulphuric
acid which is used in the preparation performs no further part than
to take up this water, which would otherwise go to dilute the rest of the
nitric acid. The union of sulphuric acid and water is attended with great
heat, hence the necessity of cooling the vessels in making the gun-cotton.
Quite other products would be formed if the mixture became heated.
The action of nitric acid on glycerine is of the same kind as that on
cellulose. When glycerine is allowed to drop into a cooled mixture of nitric
acid and sulphuric acid, the eye can detect little or no difference between
the appearance of the liquid which collects in the bottom of the vessel and
the glycerine dropped in. The product of the action is, however, the terrible
nitro-glycerine, a heavy, oily-looking liquid, which explodes with fearful
violence. Even a single drop placed on a piece of paper, and struck on
an anvil, detonates violently and with a deafening report. The chemical
change which is effected in the glycerine (C3H8O3), is the substitution of
three NO2 groups for three of hydrogen, producing C3H5(NO2)3O3, or
tri-nitro-glycerine. The general reader may perhaps marvel that the chemist
should be able not only to count the number of atoms which go to
make up the particles of a compound body, but to say that they are arranged
so and so: that the atoms do not form an indiscriminate heap, but that they
are connected in an assignable manner. The reader is no doubt aware
that these compound particles are extremely small, and he may reasonably
wonder how science can pronounce upon the structure of things so small.
He may be more perplexed to learn that a calculation made by Sir W.
Thompson shows that the particles of water, for instance, cannot possibly
be more than the 1 250000000th of an inch in diameter, and may be only 1 20th
of that size. The truth is that the very existence of atoms and molecules
is an assumption. Like the undulatory ether, it is an hypothesis which is
adopted to simplify and connect our ideas, and not a demonstrated reality.
But the atomic hypothesis has so wide a scope that some philosophers hold
the existence of atoms and molecules as almost a known fact. Be that as
it may, the chemist in assigning to a body a certain molecular formula
really does nothing but express the results of certain experiments he has
made upon it. With one re-agent it is decomposed in this manner, with
another in that. By certain treatment it yields an acid, a salt; so much
carbonic acid, such a weight of water, is acted on or remains unaltered;
gives a precipitate or refuses to do so. Such are the facts which the chemist
conceives are co-ordinated and expressed by the formula he gives to
a substance. The best formula is that which accords with the greatest
number of the properties of the body—which includes as many of the facts
as possible. It follows, therefore, that a formula which aims at expressing
more than the mere percentage composition of the body—which, in the
language of the atom hypothesis, seeks to represent the mode in which the
atoms are grouped in the molecule, but which in reality represents only
reactions, is written according as the chemist considers this or that group
of reactions more important. These remarks might be illustrated by filling
this page with the different formulæ (a score or more) which have been
proposed as representing the constitution (reactions?) of one of the best-known
of organic compounds, namely, acetic acid.
Whether atoms really exist, and their arrangement in the particles of
bodies can be deduced from the phenomena, or not, the fact is undeniable
that these ideas have given chemists a wonderful grasp of the facts of their
science. The consistency and completeness of the explanation afforded
744by these theories are ever being extended by modifications which enable
them to embrace more and more facts. Some of the properties of the
substance we are now considering confirm in a remarkable manner the
theoretical views which are expressed in its constitutional formula. We
may first consider the nature of gunpowder, and by comparing it with nitro-glycerine,
endeavour to explain the greater power of the latter substance.
Gunpowder is a mixture of charcoal, sulphur, and nitre, the latter constituting
three-fourths of its weight. Nitre supplies oxygen for the combustion
of the charcoal, which is thus converted into carbonic acid, and the
sulphur, which is added to increase the rapidity of the combustion, is also
oxidized. The products of the action are, however, numerous and complicated,
but the important result is the sudden generation of a quantity of
carbonic acid, nitrogen, carbonic oxide, hydrogen, and other gases, which
at the oxidizing temperature and pressure of the air would occupy a space
300 times greater than the powder from which they are set free; but the
intense heat attending the chemical action dilates the gases, so that at
the moment of explosion they would occupy a space at least 1,500 times
greater than the gunpowder. The materials of which gunpowder is composed
are finely powdered, in order that each portion shall be in immediate
contact with others, which shall act upon it. Plainly, the more thorough
the incorporation of the materials—that is, the more finely ground and
intimately mixed they are—the more rapid will be the inflammation of the
powder.
Looking now at the crude formula of nitro-glycerine, C3H5N3O9, the
reader will remark that the molecule contains more than sufficient oxygen
to form carbonic acid with all the carbon atoms, and water with all the
hydrogen atoms; for the C6 in two molecules of nitro-glycerine would take
only O12 to form 6CO2; and the H10, to be converted into 5H2O, would
only need O5; thus there would be an excess of oxygen. Now, it may
occur to the reflective reader that in every molecule of nitro-glycerine the
carbon and hydrogen are already associated with as much oxygen as they
can take up: that they are, in fact, already burnt, and that no further union
is possible. But from chemical considerations it has been deduced that
in the nitro-glycerine molecule the oxygen atoms, except only three, which
are partially and imperfectly joined to carbon, are united to nitrogen atoms
only. The constitution of the molecule may be represented by arranging,
as below, the letters which stand for the atoms, and by joining them with
lines, which shall stand for the bonds by which the atoms are united.
We see here that the hydrogen atoms are completely, and the carbon
atoms partially, detached from the oxygen atoms; and therefore these
atoms are in the condition of the separated carbon and oxygen atoms in
gunpowder. Only the pieces of matter which lie side by side in gunpowder
are in size to the molecules of nitro-glycerine as mountains to grains of
sand. The mixture of the materials is then so much more intimate in
nitro-glycerine, since atoms which can rush together are actually within
745the limits of the molecules; and these molecules have such a degree of
minuteness, that 25 millions, at least, could be placed in a row within the
length of an inch. We know that the finer the grains and the more intimate
the mixture, the quicker will gunpowder inflame; but here we have a
mixture far surpassing in minute subdivision anything we can imagine as
existing in gunpowder. Hence the combination in the case of nitro-glycerine
must be instantaneous, whereas that in gunpowder, quick though it be,
must still require a certain interval. If it take a thousandth of a second
for the gases to be completely liberated from a mass of gunpowder, and
only one-millionth of a second for a vast quantity of carbonic acid, nitrogen,
and steam to be set free from nitro-glycerine, the destructive effect
will be much greater in the latter case. Again, the volume of the gases
liberated from nitro-glycerine in its detonation have at least 5,000 times
the bulk of the substance. We have entered into these chemical considerations,
at some risk of wearying the reader, with the desire of affording
him a clue to the singular properties of nitro-glycerine and gun-cotton,
which we are about to describe.
The nature of the chemical changes which may be set up in an explosive
substance, and the rapidity with which these changes proceed throughout
a mass of the material, are greatly modified by the conditions under which
the action takes place. If a red-hot wire be applied to a small loose tuft
of gun-cotton, it goes off with a bright flash without leaving any smoke or
any other residue. Thus, when the substance is quite unconfined, no explosion
occurs. If the cotton-wool be made into a thread, and laid along
the ground, it will burn at the rate of about 6 in. per second; if it be twisted
into a yarn, the combustion will run along at the rate of 6 ft. per second;
but if the yarn be enclosed in an Indian-rubber tube, the ignition proceeds
at the rate of 30 ft. in a second. If to a limited surface of gun-cotton, such
as one end of a length of gun-cotton yarn, a source of heat is applied—the
temperature of which is high enough to set up a chemical change, but not
high enough to inflame the resulting gases (carbonic oxide, hydrogen, &c.)—the
cotton burns comparatively slowly, rather smouldering than inflaming.
If, however, a flame be applied, the gun-cotton flashes off with great
rapidity, because the heat applied sets fire to the gaseous products of the
chemical action. But if the gun-cotton be confined so that the gases cannot
escape, the combustion becomes rapid however set up. The reason is
that if the gases escape into the air, they carry off so much of the heat produced
by the smouldering gun-cotton, that the temperature does not rise
to the extent required to produce the flaming ignition, in which the products
are completely oxidized. If a mass of gun-cotton be enclosed in a
capacious vessel from which the air has been removed, and the gun-cotton
be ignited by means of a wire made hot by electricity, the cotton will at
first only burn in the slow way without flame; but as the gases accumulate
and exert a pressure which retards the abstraction of heat accompanying
their formation, the temperature will rise and attain the degree necessary
for the complete and rapid chemical changes involved in the flaming combustion.
Thus, the more resistance is offered to the escape of the gases,
the more rapid and perfect is the combustion and explosive force produced
by the ignition. Now, the explosion of gun-cotton has been found to be
too rapid when it is packed into the powder-chamber of a gun, for its tendency
is to burst the gun before the ball has been fairly started. Hence
a material like gunpowder, in which the combustion is more gradual, is
better suited for artillery. The ignition of gunpowder, though rapid, is not
746instantaneous, and therefore we can speak of it as more or less gradual.
Indeed, in even the most violent explosives, some time is doubtless required
for the propagation of the action from particle to particle. This
extreme rapidity of combustion, and consequent rending power, which is
so objectionable in a gun-chamber, makes gun-cotton a most powerful
bursting charge for shells, and, when it is enclosed in strong receptacles,
for torpedoes also.
But by the researches of Nobel, Professor Abel, and others, it has been
discovered—and this is, perhaps, the most remarkable discovery in connection
with explosives—that gun-cotton, nitro-glycerine, and other explosive
bodies, are capable of producing explosions in a manner quite different
from that which attends their ignition by heat. The violence of this kind
of explosion is far greater than that due to ordinary ignition, for the action
takes place with far greater rapidity throughout the mass, and is, indeed,
practically instantaneous. It appears to be produced by the mere mechanical
agitation or vibrations which are communicated to the particles of the
substance. Turning back to the representation of the molecule of nitro-glycerine
on page 744, it will not be difficult to imagine that this may be
an unstable kind of structure; that the atoms of oxygen are prevented from
rushing into union with those of hydrogen and carbon only by the interposition
of the nitrogen; and that an agitation of the structure might shake
all the atoms loose, and leave them free to re-combine according to their
strongest affinities. Nitro-glycerine is by no means so ready to inflame as
is gun-cotton: it is said that the flame of a match may be safely extinguished
by plunging it into the liquid; and when a sufficient heat is applied
to a quantity of the liquid in the open air, it will burn quietly and without
explosion. Even when nitro-glycerine is confined, the application of heat
cannot always be made to produce its explosion; or, at least, the circumstances
under which it can do so are not accurately known, and the operation
is difficult and uncertain. On the other hand, nitro-glycerine explodes
violently even when freely exposed to the air if there be exploded in contact
with it a confined charge of gunpowder, or a detonating compound
such as fulminating powder. Gun-cotton possesses the same property of
exploding by concussion, which appears indeed to be a general one belonging
to all explosive bodies. According to recent researches, even gunpowder
is capable of a detonative explosion. A mass of gunpowder confined with
a certain proportion of gun-cotton, which is itself set off by fulminate of
mercury, is said to exert an explosive force four times greater than that
developed by the ignition of the gunpowder in the ordinary manner. It
has also been found that wet gun-cotton can be exploded by concussion,
and the force of the explosion is unimpaired even when the material is
saturated with water. This makes it possible to use gun-cotton with greater
safety, as it may be transported and handled in the wet condition without
risk, and it preserves its properties for an indefinite period without being
deteriorated by the water. Some experiments illustrating the extraordinary
force of the detonative explosions of gun-cotton and nitro-glycerine will
give the reader an idea of their power.
A palisade, constructed by sinking 4 ft. into the ground trunks of trees
18 in. in diameter, was completely destroyed in some experiments at Stowmarket
by the explosion of only 15 lbs. of gun-cotton. Huge logs were
sent bounding across the field to great distances, and some of the trees
were literally reduced to match-wood. The gun-cotton, be it observed, was
simply laid on the ground exposed to the air. The destructive powers of
747nitro-glycerine are even greater. A tin canister, containing only a few
ounces of nitro-glycerine, is placed, without being in any way confined, on
the top of a smooth boulder stone of several tons weight; it is exploded
by a fuse containing fulminating powder, which is fired from a distance by
electricity. There is a report, and the stone is found in a thousand fragments.
The last experiment shows one of the advantages of nitro-glycerine
over gunpowder as a blasting material, beyond its far greater power, which
is about ten times that of gunpowder. A charge of gunpowder inserted in
a vertical hole tends to force out a conical mass, the apex of which is at
the space occupied by the charge. With nitro-glycerine, and also with
gun-cotton, which last has almost six times the force of gunpowder, a
powerful rending action is exerted below as well as above the charge.
Again, in blasting with gunpowder the charge must be confined, and the
hole is filled in above the charge with tightly rammed materials, forming
what is termed the tamping. But nitro-glycerine requires no tamping: a
small, thin metallic core containing the charge is simply placed in the
drill-hole, or the liquid itself is poured in, and a little water placed above
it. The effect of the explosion of nitro-glycerine in “striking down,” when
apparently no resistance is offered, will seem very strange to the reader
who is oblivious of certain fundamental principles of mechanics. The
force of the explosion is due entirely to the sudden production of an enormous
volume of gas, which at the ordinary pressure would occupy several
thousand times the bulk of the material from which it is produced. This
gas, by the law of the equality of action and reaction, presses down upon
the stone with the same force that it exerts to raise the superincumbent
atmosphere. The pressure of the gas at the moment of its liberation is
enormous; but the atmosphere cannot instantaneously yield to this, for
time is required to set the mass of air in motion, and the wave of compression
advances slowly compared with the rapidity of the explosion.
Hence the air acts, practically, like a mass of solid matter, against which
the gases press, and which yields less readily than the rock, so that the
blow which is struck takes visible effect on the latter. Now, with gunpowder,
the evolution of gas is less rapid, the atmosphere has time to yield,
and the reaction has not the same violence. The rapidity of the evolution
of gas from the exploding nitro-glycerine is so great, that the gases, though
apparently unconfined, are not so in reality; for the atmosphere acts as a
real and very efficient tamping.
When nitro-glycerine first came into use for blasting purposes, it was
used in the liquid form under the name of “blasting oil;” but the dangers
attending the handling of the substance in this state are so great, that it
is now usual to mix the liquid with some powdered substance which is itself
without action, and merely serves as a vehicle for containing the nitro-glycerine.
To mixtures of this kind the names “dynamite,” “dualine,”
“lithofracteur” &c., have been given.
It is now hardly necessary to point out that the discovery of these new
explosives has largely extended our power over the rocks, enabling works
to be executed which would have been considered impracticable with less
powerful agents. It is true that the most fearful disasters have been accidentally
produced by the new explosives; but such occasional devastation
is the price exacted for the possession of powerful agents. And just as in
other cases—steam, for example—where great forces are dealt with, so
these new powers must be managed with unceasing care, and placed in
the hands of only skilful and intelligent men.
748The products of the combustion of gunpowder are not all gaseous, but
include solid compounds, such as carbonate and sulphate of potassium.
It is these that give rise to the smoke seen when a gun is discharged, and
which, in rapid firing, soon obscures the sight of the objects aimed at.
They are also the causes of the fouling of the bore. Gun-cotton is quite
unexceptionable in these respects, and that prompted the attempts made
soon after its introduction to use it instead of gunpowder in fire-arms.
But the explosion of gun-cotton was found too sudden and violent for
guns and rifles, so that many serious accidents in consequence occurred.
The next thing done was to lessen the rapidity of the explosion by using
gun-cotton mixed with ordinary cotton, or twisted in threads round some
inert substance—in fact, to mitigate the violence of the shock by some
mechanical disposition of the material. The introduction of rapid firing
guns and repeating rifles forced on the problem of a smokeless powder;
and as the plan of replacing nitrate of potassium, in ordinary gunpowder,
by nitrate of ammonium was found to be attended with loss of the keeping
quality of the powder, other materials, such as picric acid, which forms
also the basis of the explosive called mélinite, have been proposed. The
composition of mélinite was long a mystery, and that of the smokeless
powder adopted by the French was so carefully concealed that many experiments
had to be made by other nations to discover some similar preparation,
which was found possible by combining certain substances with
gun-cotton so as to modify the violence of its explosion, and produce a
manageable material having the required properties. The British Government,
after many experiments and much careful testing, decided to adopt
cordite, made of nitro-glycerine, in which, by the aid of volatile solvent,
di-nitro-cellulose is dissolved, together with a little mineral oil. The semi-fluid
composition, forced through a round hole or die, comes out like
a thread or cord, which the evaporation of the volatile solvent leaves
with very much the appearance of common brown window-cord.
This material has the several advantages of keeping well, of being uniform
in its propulsive powers, of being capable of imparting as high a velocity
as a much larger charge of the ordinary black gunpowder, while at the
same time exercising a less pressure on the chase of the gun.
It will have become obvious from the preceding paragraphs that,
according to the conditions under which an explosive is to be used,
selection must be made of the most suitable. For example, the substances
employed for propelling projectiles from guns must not have the
violent rending power of certain others, which, by this very property,
are most useful for blasting operations; and, again, although explosives
of this last kind are inadmissible as projectile agents, they are of the kind
best adapted for use in shells where it is the disruptive action that is required.
Also in blasting operations, the explosive has to be adapted to
the nature of the work, and it has been found that a substance which has
worked well in driving a heading for a tunnel through one kind of rock
may prove both slow in progress, and more costly in expenditure, when
some different kind of rock is reached. Besides this, regard must be had
in blasting operations to the nature of the effect required, which is in
some instances a shattering of the rock into fragments, in others a
detachment of it in masses. Thus, in the working of a slate quarry, the
explosive used must not be of a nature to shiver the rock into useless
splinters, but must operate in such a manner that compact masses may
be separated from the mountain side in a condition suitable for cleaving,
by appropriate tools, into numberless broad laminæ, which, trimmed
749into rectangular shape, constitute our well-known roofing slates. The
blasting used on a coal seam must be so conducted as to yield the
material as much as possible in big lumps or cobbles rather than in
slack. When granite is blasted for the purpose of obtaining building
stones, the explosive must be one that, by its comparatively slow action,
divides the compact rock into the largest possible blocks. On the other
hand, when granite is blasted merely with the object of removing it, as
when a tunnel has to be driven through a mass of it, the most disintegrating
agent is then the best. The common popular expressions by
which the two classes of explosives just referred to are distinguished are
“high explosives” and “low explosives.” Dynamite may be taken as a
type of the former, and gunpowder a type of the latter. As will be
gathered from what is to follow, no definite separation between these
classes can be fixed, but in a general way it may be said that, where a
destructive, rather than a propelling or pressure effect is required, the
explosive used is one brought into operation by a concussive or detonating
priming, and acting mostly by detonation within itself, such as
dynamite, &c.
Whereas, up to nearly the middle of the nineteenth century, gunpowder
was practically the only explosive in use for either civil or military
purposes, the close of the century can show a list of several hundred preparations
that have been proposed or actually used in its stead. The
names by which these are put forward are expressive sometimes of
an ingredient in their composition, such as “ammonia dynamite,”
“cellulosa,” “mica powder,” “dynamite au carbon,” “dynamite de boghead,”
&c.; and sometimes the inventor’s name, as “So-and-so’s powder
or explosive”; sometimes of the strength of the mixture under various
fanciful names, such as “dynamite,” “heraklin,” “vigorite,” &c., &c.;
sometimes the names relate to the appearance of the compound, as
“white gunpowder,” “blasting gelatine,” &c., &c.; and sometimes to
other circumstances, such as “pudrolithe,” “saxifragine,” “safety
powder,” &c., &c. A very long list might be given of the substances
severally used in these various compositions. It will be sufficient to
indicate the general nature of the several classes into which the new
explosives may be divided. By turning back to p. 746, the reader will be
reminded of the composition of gunpowder, and of the part played
therein by the nitre (nitrate of potassium). Now a considerable number
of the recently patented explosives are simply modified gunpowders,
which all contain some nitrate, replacing wholly, or in part, the nitrate of
potassium, while sulphur is an ingredient of nearly all, and in many, the
charcoal of gunpowder is partly or wholly replaced by other carbonaceous
materials, such as sawdust, coal-dust, tan, starch, paraffin, lycopodium,
graphite, peat, flour, bran, &c. Certain mineral salts enter into the composition
of some, such as sulphate of iron, carbonate of copper, sulphide
of antimony, &c., &c.
In another class of the newer explosives chlorate of potassium takes
the place of the nitrate as the oxygen supplying material, with similar
variations as to the carbonaceous matter as are referred to above.
Yellow prussiate of potash and sugar sometimes replace both the charcoal
and sulphur of gunpowder in this class. Explosives of this chlorate
class are usually dangerous to manufacture, and are often very sensitive,
and also liable to changes by keeping, which render them still more
dangerous.
750The next class of preparations brings us to the “high explosives,”
properly so called, and it is among these that most notable preparations
are met with. Of all the explosive nitro-compounds, gun-cotton was the
first practically employed (vide p. 741); but very soon after nitro-glycerine
was discovered by Sobrero when working in Pelouze’s laboratory.
This afterwards became known as “blasting oil,” but it was many
years before nitro-glycerine came into use as an explosive, namely, when,
about 1860, Nobel, a Swedish engineer, had established factories for its
production as an agent for blasting. At first there were difficulties and
dangers attending its use, and it was only when Nobel had discovered
the detonation method of setting free its tremendous energy that the
new era of “high explosives” really commenced. Between 1860 and
1870 such a number of appalling catastrophes occurred in the handling of
the new “blasting oil” that in several European countries its use was
entirely prohibited. And, in England at least, this prohibition remains,
for “in a liquid state this explosive cannot be sold in, or imported into
this country. It is manufactured under the strict provision that it is
forthwith made up into dynamite or some kindred licensed explosive.” ...
“The only source, practically speaking, of nitro-glycerine on a
commercial scale in this country is the factory of Nobel’s Explosive Co.
(Ltd.) at Ardeer, in the county of Ayr.”[17] Nitro-glycerine being so extremely
dangerous to handle in the liquid form led Nobel to propose its
use in an altered condition, by causing it to be absorbed by some inert
porous material, the most suitable being a siliceous earth found in
Germany, and there known as kieselguhr, of which one part will absorb
three times its weight of liquid nitro-glycerine. Here we have the
original dynamite, but now other substances are used for absorbing the
liquid, and there are, indeed, dynamites of two different classes:
1. Dynamites with inert absorbents.
2. Dynamites with absorbents which are themselves combustible, or
explosive.
17. Major Cundill, H.M.’s Inspector of Explosives.
Of the latter class there are endless varieties. One that has latterly
been much used is called “blasting gelatine,” and is practically a combination
of nitro-glycerine and nitro-cotton, this last ingredient being a
less nitrated cellulose than gun-cotton. Blasting gelatine contains a very
large percentage of nitro-glycerine (93–95 per cent.), and has the appearance
of stiff jelly of a pale yellow colour. It may be of interest to remark
that this second class of dynamites admits of well-defined sub-divisions
according to the nature of the absorbent, as:
(a) Charcoal, or other simple carbonaceous material.
(b) Gunpowder, or other nitrate or chlorate mixtures.
(c) Gun-cotton, or other nitro-compounds.
751
Fig. 340.—View on the Tyne.
MINERAL COMBUSTIBLES. — COAL. — PETROLEUM. — PARAFFIN.
Certain mineral combustibles may fairly claim attention in a work
treating of the discoveries of the nineteenth century, not because these
bodies have been known and used only in recent times, but for other reasons.
The true nature of coal—that most important of all combustibles—its
relation to the past history of the earth, and to the present and future
interests of mankind; the work it will do; the extent of the supply still
existing in the bowels of the earth; the innumerable chemical products
which it yields—are subjects on which the knowledge gained during the
present century forms a body of discovery of the most interesting and
important kind. Another substance we have to mention, though not a
modern discovery, has lately been found in far greater abundance, and is
now so largely used for various purposes, that it has become an important
article of commerce.
Fig. 341.—Fossil Trees in a Railway Cutting.
Most persons know, or at least have been told, that coal is fossil
vegetable matter,—the long-buried remains of ancient forests. But
752probably many receive the statement, not perhaps with incredulity, but
with a certain vague notion that it is, after all, merely a daring surmise.
And, indeed, nothing is at first sight more unlike stems, or leaves, or roots
of plants than a lump of coal. Then everybody knows that coal is found
thousands of feet beneath the surface of the earth, whereas plants can
grow only in the light of the sun. One begins to understand the matter
only when the teachings of geology have shown him that, so far from the
crust of the earth being, as he is apt to suppose, fixed and unchangeable,
it is in a state of constant fluctuation. Changes in the levels of the ground
are always going on: in one place it is rising, in another sinking; here a
tract of land is emerging from the ocean, there a continent is subsiding
beneath the water. The extreme slowness with which these changes proceed
causes them to escape all ordinary observation. The case may be
compared to the hour-hand on the dial, which a casual spectator might
pronounce quite stationary, since the observation of a few seconds fails to
detect its movement. As the whole period comprehended in human annals
counts but as a second of geological time, it cannot be wondered at that
it required a vast accumulation of facts, and much careful and patient
deduction from them, before a conclusion was reached so apparently contradictory
of experience. It is, indeed, startling to learn that “the sure
and firm-set earth” is in a state of flow and change. Even the “everlasting
hills” give evidence that their materials were collected at the bottom
753of the sea, and we know that the water which runs down their sides is
slowly but surely carrying them back particle by particle. Of the magnitude
of the changes which the surface of the earth has undergone in times
past, and which are still imperceptibly but constantly proceeding, the ordinary
experience of mankind can of itself give no example. But such changes
have sufficed to entomb a vast quantity of relics of the innumerable forms
of vegetation which flourished and waved their branches in the sun, ages
upon ages before the advent of man.
Fig. 342.—Impression of Leaf found in Coal Measures (Pecopteris).
It may be thought impossible that vegetable matter should have so
changed as to become a dense, black, glistening, brittle mass, showing no
obvious forms of leaves or texture of wood. But no one who has seen
how a quantity of damp hay closely pressed together will, after a time,
become heated and change in colour to black, can have any difficulty in
comprehending how chemical and mechanical actions may completely
alter the aspect of vegetable
matter. We have, however,
the most direct evidence of
the vegetable origin of coal in
the numberless unquestionable
forms of trees and plants
met with in all coal strata.
Sometimes the trunks of the
trees fossilized into stony matter
are found upright in the
very situation in which they
grew. Thus in Fig. 341 is represented
the appearance exhibited
by the trunks and roots
of some fossil trees, which
were exposed to view in the
formation of a railway cutting
between Manchester and
Bolton. In every coal-field
also beautiful impressions of
the stems and leaves of plants
are met with—one common
form of which is shown in Fig.
342. Most of the plants so
found belong to the flowerless
division of the vegetable
kingdom. Some are closely
allied to the ferns of the present
day—to the common “mare’s-tail” (Equisetum), to the club-moss, and
to other well-known plants. The firs and pines of the coal age are scarcely
distinguishable from existing species. If a fragment of ordinary coal be
ground to a very thin slice—so thin as to be transparent—and placed
under the microscope, it will show a number of minute rounded bodies,
which are, there is good reason to believe, nothing else than the spores or
seeds of plants, closely resembling the existing club-mosses. The spores
of the club-moss (Lycopodium) are so full of resinous matter, that they
are used for making fireworks and the flashes of lightning at theatres. It
is, therefore, extremely probable that the bitumen of coal is due to the
resin of similar spores, altered by the effects of subterranean heat. The
754immense abundance of these little spores in the coal is a proof that they
accumulated in the ancient forests as the mosses grew, and therefore the
matter of coal was not accumulated under water or washed down into the
sea; for these little spores are extremely light, and they cannot be wetted
by water, and therefore they would have floated on the surface, and would
not have been found so diffused throughout the coal. Fig. 343 is a picture
of the possible aspect of the ancient forests of the coal age. In the humid
atmosphere which probably prevailed at that period, the large tree-ferns
and gigantic club-mosses, which are conspicuous in the picture, must have
flourished luxuriantly.
Fig. 343.—Possible Aspect of the Forests of the Coal Age.
The immense importance of coal for domestic purposes will be obvious
755from the fact that it is estimated that in the United Kingdom alone no less
than 30,000,000 tons are annually consumed in house fires. Another great
use of coal is in the smelting, puddling, and working of iron, and this probably
consumes as much as our domestic fireplaces. Then there is the
vast consumption by steam engines, by locomotives, and by steamboats.
Another purpose for which coal is largely used is the making of illuminating
gas; and to the foregoing must also be added the quantity which goes
to feed the furnaces necessary in so many of the arts—such as in the
manufacturing of glass, porcelain, salt, chemicals, &c. The quantity of
coal raised in Great Britain was not accurately known until 1854, when it
was ordered that a register should be kept, and an annual return made.
The following figures, in round numbers, are the returns published up to
1873. The table is continued in Note A.
Year.
Coal raised, in Tons.
1854
64,661,000
1855
64,453,000
1856
66,645,000
1857
65,395,000
1858
65,008,000
1859
71,979,000
1860
83,208,000
1861
85,635,000
1862
83,638,000
1863
88,292,000
1864
92,787,000
1865
98,150,000
1866
101,630,000
1867
104,500,000
1868
103,141,000
1869
107,427,000
1870
110,289,000
1871
117,352,000
1872
123,497,000
1873
127,017,000
The first return showed our annual produce to be 64,661,000 tons. The
amount did not greatly vary until 1859, when there was an increased
production of nearly seven millions of tons; in 1860 a further increase of
eleven millions of tons more. Since then the quantity annually raised has
been increasing. Comparing the quantity which has been raised in any
year after 1863 with that raised ten years before, we see that the increase
in ten years is nearly half as much again; or, that at the present rate of
increase the amount annually raised doubles itself at least every twenty
years. Now, the question arises, How long can this go on? However
great may be the store of coal, it must sooner or later come to an end. Is
it possible to calculate how long our coals will last? and what are the
results of such calculations? These calculations have been made; but
there are great discrepancies in the results, for the estimates of the amount
of available coal still remaining vary greatly, and different views are held
regarding the rate of consumption in the future. A very liberal estimate,
by an excellent authority, of the quantity of coal remaining under British
soil, makes it 147,000 millions of tons. With a consumption stationary at
the present rate, this will last 1,200 years; with an increase of consumption
of 3,000,000 tons a year, 276 years; but if the consumption continues to
increase in the same geometrical ratio it has hitherto followed, the supply
will scarcely last 100 years. It cannot be conceived, however, that this
last will be the real case, for the increasing depth to which it will be necessary
to go will soon cause a great increase in the cost, and thus effectually
check the consumption. Great Britain will, however, be compelled to
retire from the coal trade altogether, by the cheaper supplies which other
countries will yield, long before the absolute exhaustion of her own coal-fields.
It is calculated that the coal-fields of North America contain thirteen
times as much as those of all Europe put together. Coal is also found
756abundantly in India, China, Borneo, Eastern Australia, and South Africa;
and it is believed that these stores will supply the world for many thousand
years.
Fig. 344.—The Fireside.
Seeing, then, that our supply of coal has a limit, and that at the present
increasing rate of consumption, the chief source of the wealth of Great
Britain must necessarily be exhausted in a few more centuries, it behoves
us to turn our mineral treasures to the best account, and to adopt every
possible means of obtaining from our coal its whole available heat and
force. The amount of avoidable waste of which we are guilty in the consumption
of coal is enormous. This is especially the case in its domestic
use, where probably nineteen-twentieths of the heat produced is absolutely
thrown away—sent off from the earth to warm the stars. In England
people look upon the wide open fireplace as the image and type of home
comfort. No doubt there are, from long use and habit, many pleasing associations
which cluster round the domestic hearth; but we, to whom it is
given to “look before and after,” must think what it takes to feed that wide-throated
chimney. All but a very small fraction of the heat thus escapes,
and is lost to man and the world for ever; and surely we shall deserve the
curses of our descendants if we continue recklessly to throw away a treasure
which, unlike the oil in the widow’s cruse, is never renewed—for there is
no contemporaneous formation of coal. Thanks to the enhanced price of
coal during the last few years, some attention has been directed to contrivances
757for the economical consumption of coal in its domestic, as well
as in its manufacturing, applications.
A time, however, will sooner or later come, when the whole available
coal shall have been consumed. What will then be the fuel of the engines,
and steamboats, and locomotives of the future? The reader may think
that then it will only be necessary to burn wood. But wood is already
being consumed from the face of the earth much more rapidly than it is
produced. How, then, can it be available when coal fails? The truth is,
we are now consuming not merely the wood which the sun-rays are building
up in our own time, but in hewing down the forests we are using the
sun-work of a century, while in coal we have the forests of untold ages at
our disposal—the accumulated combustible capital stored up during an
immense period of the earth’s existence. Upon this stored-up capital we
are now living, our current receipts of sun-force being wholly inadequate
to meet our expenditure. The coal is the sun-force of former ages; and it
is from this we are now deriving the energy which performs most of our
work. George Stephenson long ago declared that his locomotives were
driven by sunshine—by the sunshine of former ages bottled up in the coal.
And he was right. The mechanical energy of our steam engines, and the
chemical energy of our blast furnaces, are derived from the combustion of
vegetable matter, in which the heat and light of the sun—our present sun
or that of the coal ages—are in some way stored up. The burning of wood
or coal is, chemically, the reverse action to that performed by the sunlight:
by the former carbon and oxygen are united, by the latter they are
separated.
We foresee, then, a future period—however distant may be that future—in
which the world’s capital shall have been exhausted, and the energies
which are now employed in doing the world’s work will no longer be available.
But the reader will perhaps think that by improvements in the steam
engine, and in other ways, means will be found of getting more and more
work out of coal. It is true that we obtain from coal only a fraction of its
available energy; but the whole work which could, by any possible process,
be done by the combustion of coal is definite and limited, although its
amount is large. A pound of coal burnt in one minute sets free an amount
of energy which would, if it could all be made available, do as much as
300 horses working in the same time. But, again, the reader may think,
even if at some distant future the supplies of fuel for the steam engines of
our remote posterity should fail, that before that time some other form of
force than steam or heat engines will have been discovered—some application
of electricity, for example. Now, it will appear, from principles which
will be discussed in a subsequent article, that not only is there no probability
of such a discovery, but that now, when the relations of the whole
available energies of the globe have been traced and defined, Science can
find no ground for admitting such a possibility under the present condition
of the universe.
When coal is heated in closed vessels, there are given off, as we shall
presently see, a number of gaseous and volatile products—many
being compounds of carbon and hydrogen—which condense to liquids or
758solids at ordinary temperatures. Carbon is by far the largest constituent
of coal, which commonly contains only about 10 per cent. of other substances,
although the proportions vary very widely. Another important
constituent of coal is its hydrogen, and the value of coal as a source of
heat depends almost entirely upon the carbon and hydrogen it contains.
Carbon is one of the most remarkable of all the elements of the globe for
its power of entering into an enormous number of compounds. Thus, for
example, the compounds of carbon with only hydrogen are innumerable;
but they are all definite, and their composition is expressible by the admirable
system of chemical symbols, of which the reader has now, it is hoped,
some definite notion. Perhaps these hydro-carbons are among the best
evidences which could be adduced that modern science has obtained a
grasp of certain conceptions which have a real correspondence with the
actual facts of nature, even as regards the intimate constitution of matter.
This is not the place to enter into a complete exposition of this subject.
We may, however, invite the reader’s attention to a few simple facts. A
very large number of compounds of carbon and hydrogen are known. If
the percentage compositions of these be compared together, it is only the
eye of a most expert arithmetician which can detect any relation between
the proportions of the constituents in the various compounds. The chemist,
however, by associating such of these compounds as resemble each
other in their general properties, finds that they can be arranged in series,
in which the composition is accurately expressed by multiples of the proportions:
C = 12, H = 1. And not only so, the different series themselves
form a series of series, having a simple relation to each other. Thus, confining
ourselves to some of the known hydro-carbons, we have the following:
A
B
C
D
E
F
C H4
C H2
C2H6
C2H4
C2H2
C3H8
C3H6
C3H4
C3H2
C4H10
C4H8
C4H6
C4H4
C4H2
C5H12
C5H10
C5H8
C5H6
C5H4
C5H2
C6H14
C6H12
C6H10
C6H8
C6H6
C6H4
&c.
&c.
&c.
&c.
&c.
&c.
CnH2n + 2
CnH2n
CnH2n – 2
CnH2n – 4
CnH2n – 6
CnH2n – 8
This table might be indefinitely extended, but enough is given to enable
the intelligent reader to discover the laws connecting these formulæ. The
series headed B, it will be observed, have all the same percentage composition.
Why, then, one formula rather than another? The answer to this
question is the statement of a theoretical law upon which the whole science
of modern chemistry is based; for it has the same relation to that science
as gravitation has to astronomy. It is a matter of fact that all gases, whatever
their chemical nature, expand alike with the same application of heat,
and all obey the same law, which connects volumes and pressures. These
are very remarkable uniformities, for gases in this respect exhibit the most
decided contrast to liquids and solids. The volume of each solid and of
each liquid has its own special relations to temperature and pressure: here
759there is endless diversity. The volumes of all gases have one and the same
relation to temperature and pressure: here there is absolute uniformity.
As an explanation of these and other facts relating to gases, Amedeo
Avogadro, in 1811, put forward this hypothesis—Equal volumes of all
gases, under like circumstances of temperature and pressure, contain the
same number of molecules. This hypothesis was revived by Ampère a few
years later, and sometimes is called his. A necessary consequence of this
law is that the weights of the molecules of gases are proportional to their
densities or specific gravities. Hence when the percentage composition of
a hydro-carbon has been determined, by burning or oxidizing it in such a
manner as to obtain and weigh the products, carbonic acid and water, the
next thing the chemist does is to obtain the weight of a volume of the gas.
The number of times this exceeds the weight of hydrogen gas, under the
same conditions, expresses how many times the molecule is heavier than
the hydrogen molecule. Now, the chemist’s unit of weight in these inquiries
is the weight of a single atom of hydrogen; and, as there are grounds for
believing that the molecule of hydrogen consists of two atoms of that substance,
its weight = 2. Now, if the molecule of marsh gas, the first hydro-carbon
in the above list, has the composition assigned, it will be 12 + 4 = 16
times heavier than the atom of hydrogen, and 16 2 = 8 times heavier than
the molecule of hydrogen. Hence, if Avogadro’s law be correct, marsh gas
should be just eight times heavier than hydrogen gas; which is really the fact.
The formula expressing the composition of the molecule of a hydro-carbon,
or of any chemical compound whatever, is always so fixed that the same
relations may hold; and almost the first thing a chemist does in examining
a new body is to endeavour to obtain it in the state of gas.
The first four members of the series headed A are gases at ordinary
temperatures, the fifth is a gas at temperatures above the freezing-point,
and a liquid at lower temperatures; the next following members are liquids
which boil (that is, are converted into gases) at temperatures rising with
each additional carbon atom about 20° F. The specific gravities and boiling-points
of these liquids augment as we pass from one hydro-carbon to the
next, and the lower members of the series are solids, fusing at temperatures
higher and higher as the number of carbon atoms is greater. Similar
gradations of properties are exhibited by the other series of hydro-carbons.
Petroleum or rock-oil is the name given to liquid hydro-carbons found in
nature, and consisting chiefly of compounds belonging to the series marked
A in the above list. Some varieties of petroleum hold in solution other
hydro-carbons, and in some cases paraffin is extracted from the oils by
exposing the liquid to cold, when the solid crystallizes out. Paraffin is a
solid belonging to the B series, and it is for the most part obtained by
heating certain minerals.
Deposits of liquid hydro-carbons, perhaps formed by a kind of natural
subterranean distillation from coal or other fossil organic matter, exist in
various localities. These deposits have long been known and utilized at
Rangoon, in Burmah, and on the shores of the Caspian Sea. At Rangoon
the mineral oil is obtained by sinking wells about 60 ft. deep in a kind of
clay soil, which is saturated with it. The oily clay rests upon a bed of slate
also containing oil, and underneath this is coal. It may be supposed that
subterranean heat, acting upon the coal, has distilled off the petroleum,
which has condensed in the upper strata. This petroleum, when distilled
in a current of steam, leaves about 4 per cent of residue, and the volatile
portion contains about one-tenth of its weight of a substance (paraffin)
760which is solid at ordinary temperatures. After an agitation with oil of
vitriol, and another distillation, rock oil or naphtha is obtained, which,
however, is still a mixture of several distinct chemical compounds. Mineral
oils have also been found in China, Japan, Hindostan, Persia, the West
India Islands, France, Italy, Bavaria, and England. In one of the Ionian
Islands there are oil-springs which have flowed, it is said, over 2,000 years.
But it is the recently discovered and extremely copious springs and wells
in Pennsylvania and Canada which have given a vastly extended importance
to the trade in mineral oil. Rock oil is now used in enormous quantities
as the cheapest illuminating oil, and that which furnishes the most
intense light. Its consumption as a lubricating oil for machines has also
been very large. Mineral oil was occasionally found at various places in
the United States, and sometimes used by the inhabitants of the locality
before the recent discoveries; but it was not until August, 1859, that it was
met with in large quantities. About this time a boring which was made at
Oil Creek, Pennsylvania, reached an abundant source, for 1,000 gallons a
day were drawn from it for many weeks. The news of the discovery of this
copious oil-spring spread rapidly: thousands of persons flocked to the
neighbourhood in hopes of easily making a fortune by “striking oil.” Before
the end of 1860 more than a thousand wells had been bored, and some
of these had yielded largely. The regions of North America in which
petroleum has been found cover a large part of the States, and comprise
Pennsylvania, New York, Ohio, Michigan, Kentucky, Tennessee, Kansas,
Illinois, Texas, and California. In the vicinity of Oil Creek the bore-holes
are usually about 3 in. or 4 in. in diameter, and are often 500 ft. deep, and
even 800 ft. is not uncommon. To make a bore-hole 900 ft. deep, and procure
all the requisites—steam engines, barrels, &c., for pumping the oil—costs
about $5,000. In 1869 many of these wells still yielded regularly
300 barrels a day, but the supply has not continued with the same abundance.
One of the luckiest wells flowed at its first opening at the rate
of about 25,000 barrels a day. The apparatus used for working the oil-wells
is very simple—a rude derrick, a small steam engine, a pump, and
some barrels and tubs being all that is necessary. Fig. 345 will give the
reader an idea of the scene presented by a cluster of oil-wells in the Oil
Creek region. Oil Creek received its name before the petroleum trade was
established, from the oil found floating on the surface of the water. It is on
the Alleghany River, about 150 miles above Pittsburg, and here at its mouth
is situated Oil City. There is a wharf in Pittsburg for the oil traffic, and
the barrels are brought down the river in flats, or the oil is poured into
very large flat boxes, divided into compartments, which are then closed,
and the boxes floated down in groups of twenty or more. The refining
process consists in placing the crude oil into a large iron retort, connected
with a condenser formed of a coil of iron pipes, surrounded by cold water.
Heat is applied, and the lighter hydro-carbons (naphtha) come over first.
After the naphtha, the oils which are used for illuminating purposes distil
off. A current of steam is then forced into the retort, and this brings over
the heavy oils which are used for greasing machinery. A black tarry oil
yet remains; and, finally, after the separation of this, a quantity of coke.
The products are subjected to certain processes of purification, which need
not here be described. The magnitude of the American oil trade may be
inferred from the fact that in the second year of its existence, from January
to June, 1862, more than 4,500,000 gallons were exported from four seaports.
This can hardly be wondered at, considering the extremely low
761price at which this excellent illuminating and lubricating agent can be produced.
Refined petroleum can be bought at Pittsburg for 16 cents. per
gallon. It is believed by some that the supplies of petroleum which exist
in various localities are so abundant that they will furnish illuminating oils
to the whole world for centuries.
Fig. 345.—View on Hyde and Egbert’s Farm, Oil Creek.
In the course of some researches on the substances contained in the tar,
which is obtained by heating wood in close vessels, Reichenbach found
a white translucent substance, to which he gave the above name, because
it was not acted upon by any of the ordinary chemical reagents, such as
sulphuric acid, nitric acid, &c. This substance, which is composed of
carbon and hydrogen only, is not unlike spermaceti; it is colourless, translucent,
and without smell or taste. But when slightly warmed, it becomes
very plastic, and may then be moulded with the greatest ease—and in this
respect it differs from spermaceti. Paraffin melts at from 88° to 150° C.,
to a colourless liquid, which is so fluid that it may be filtered through paper
like water, and at a higher temperature it can be distilled unchanged.
Paraffin does not dissolve in water, and is but slightly soluble in alcohol.
In ether, naphtha, turpentine, benzol, and sulphide of carbon, it dissolves
very readily. When heated with sulphur, it is decomposed: the sulphur
seizes upon its hydrogen, sulphuretted hydrogen is given off, and the
carbon is separated; and this action has been proposed as a ready means
of obtaining pure sulphuretted hydrogen for laboratory use. It is probable
762that paraffin is a mixture of various hydro-carbons, having a composition
expressible by the formula, CnH2n; for different specimens fuse at
different temperatures, according as the paraffin has been obtained from
one or the other source.
In the year 1847, Dr. Lyon Playfair directed the attention of Mr. James
Young, then of Manchester, to a dense petroleum which issued from the
crevices of the coal in a Derbyshire mine. It was soon found that this
substance yielded a distillation—a pale yellow oil—which, on cooling, deposited
solid paraffin. Mr. Young, recognizing the importance of this discovery,
had an establishment at once erected on the spot, and the work of
extracting paraffin was carried on until the supply of the petroleum had
become nearly exhausted. Forced to seek for other sources of paraffin,
Mr. Young was fortunate enough, after many trials, to discover that a
species of bituminous coal, which occurs at Boghead, near Bathgate, in
the county of Linlithgow, yielded by distillation annually large quantities
of paraffin. In 1850 he procured a patent for “treating bituminous coals
to obtain paraffin, and oil containing paraffin, therefrom.” This method
consisted in distilling the coal in an iron retort, gradually heated up to low
redness, and kept at that temperature until the volatile products ceased
to come off. Under this patent, Mr. Young developed the manufacture of
paraffin into a new and important branch of industry. The oil which first
comes over in the distillation of the Boghead mineral is largely used for
illuminating purposes under a variety of names besides that of paraffin oil,
which term is, we believe, chiefly applied to a less volatile portion, extensively
used for lubricating machinery, and consisting of liquid hydro-carbons
of the same percentage composition as solid paraffin, which substance it
also holds in solution. Mr. Young’s process consisted in placing the mineral
in a retort encased in brickwork—an arrangement which caused the temperature
of the retort to be more uniform than if the heat of the furnace
had been applied to it directly. The retorts were placed vertically, and they
were fed with the mineral by a hopper at the top. The products of the
distillation passed through a worm tube surrounded by cold water into a
cooled receiver. The result of the first distillation was a crude oily matter,
differing from tar in being lighter than water, and in not drying-up when
exposed to the air. This crude oil was then several times alternately treated
with sulphuric acid and caustic potash, and distilled; and when about two-thirds
of the oil had been separated from the rest, as an oil for burning
and lubricating purposes, the residue yielded paraffin, or “paraffin wax,”
as it is sometimes called. It is estimated that in Scotland no less than
800,000 tons of shale are annually distilled for mineral hydro-carbons, with
a consumption of 500,000 tons of fuel. It is believed that about 25,000,000
gallons of crude oil are thus obtained, and from this 350,000 gallons of
illuminating oil, 10,000 tons of lubricating oil, and 5,800 tons of solid
paraffin are produced. Among the products exhibited in the International
Exhibition of 1862, was a block of beautifully translucent paraffin, of nearly
half a ton weight.
Paraffin is also obtained on the continent by distilling a variety of coal
termed lignite. The tar which comes over is distilled, until nothing but
coke remains. The condensed products are then treated with caustic soda,
in order to remove carbolic acid and other substances. After washing with
water, the oils are treated with sulphuric acid, in order to remove basic
substances. The oil is again washed, and is then rectified by another distillation.
The products which successively come over are, if necessary,
763separated by being collected in different vessels; but sometimes they are
mixed together, and sent into the market as illuminating oils under various
names, such as “photogen,” “solar oil,” &c. Oils having a specific gravity
about 0·9 are collected apart, and are placed in tanks in a very cool place.
In the course of a few weeks the solid paraffin, which is dissolved in the
other hydro-carbons, crystallizes out. The liquid oils are drawn off, and the
crude paraffin, which is of a dark colour, is freed from adhering oil by a
centrifugal machine, and afterwards by pressure applied by hydraulic
power. It then undergoes several other processes of purification before it
is obtained as a colourless translucent solid.
Several thousand tons of paraffin are annually consumed for making
candles, which is the most important application of the material. The
variation in the fusing-points of different specimens is doubtless due to
admixtures in greater or less proportion of other more easily fusible hydro-carbons.
It was on account of the imperfect separation of these that the
candles first made from paraffin were so liable to soften and bend, and felt
greasy to the touch. Paraffin for candle-making is sometimes mixed with
a certain proportion of other substances, such as palmitic acid, &c. Among
the patented applications of paraffin are the lining of beer-barrels, and the
preserving of fruits, jams, and meat. Some kinds of paraffin are also used
in the manufacture of matches.
Liebig once expressed a wish that coal-gas might be obtained in a solid
form: “It would certainly be esteemed one of the greatest discoveries of
the age if any one could succeed in condensing coal-gas into a white, dry,
odourless substance, portable and capable of being placed in a candlestick
or burned in a lamp.” Now, it is curious that paraffin has nearly the same
composition as good coal-gas: it burns with a bright and smokeless flame,
and beautiful candles are formed of it, which burn like those made of the
finest wax. When the fused paraffin first assumes the solid form, it is transparent
like glass; and if it could be retained in that condition, we might
have the pleasing novelty of transparent candles. But the particles seek
to arrange themselves in crystalline forms, and the substance soon takes
on its white semi-opaque appearance.
The great richness of the Boghead mineral in paraffin, which appears
to exist in it ready formed, prevented for many years any successful competition
by the working of other sources of supply. But paraffin is an
abundant constituent of Rangoon petroleum, and considerable quantities
may be obtained by distilling peat, and other fossil substances. All petroleums
and paraffins are, in fact, mixtures of a number of hydro-carbons,
which in many cases cannot be entirely separated from each other. The
accidents which have from time to time occurred with some of these combustibles,
and have caused legislative enactments with regard to them, are
due to the imperfect removal by distillation of the more volatile bodies,
which rise in vapour at ordinary temperatures. Explosions of the hydro-carbons
can occur only under the same circumstances as with coal-gas;
that is to say, the application of a flame to a mixture of the vapour with
atmospheric air.
764
Fig. 346.—View of the City of London Gas-works.
COAL-GAS.
When coal is burning in a common fire, we may see jets of smoky
gas issuing from the pieces of coal before they become red hot. This
vapour, coming in contact with flame in another part of the fire, may often
be observed to ignite, thus supplying an instance of gas-lighting in its most
elementary form. In the ordinary fire the air has free access, and the
inflammable gases and vapours continue to burn with flames more or less
bright, and when these have ceased the carbonaceous portion continues
afterward to glow until nearly the whole has been consumed, except the
solid residue which we call the ashes. These ashes in general contain a
portion of unconsumed carbon, mixed with what is chemically the ash,
namely, certain incombustible salts, constituting the white part of the
ashes. If, however, we heat the coal in a vessel which prevents access of
air, and allows the gases to escape, the coal is decomposed much in the
same way as when it is burnt in the open fire; but the products formed are
no longer burnt, the supply of oxygen being cut off. Every one knows the
familiar experiment of filling the bowl of a common clay tobacco-pipe with
powdered coal, then covering it with a dab of clay, and placing it in a fire.
The gas which soon comes from the stem of the pipe does not take fire
unless a light be applied, when it may be seen to burn with a bright flame,
and after the flow of gas has ceased, nearly the whole of the carbon of the
coal will be found unconsumed in the bowl of the pipe. This simple experiment
illustrates perfectly the first step in the manufacture of coal-gas,
namely, the process of heating coal to redness in closed vessels, by which
operation the substances originally contained in coal are destroyed, and
their elements enter into new combinations.
765These elements are few in number; for, except the very small portion
which remains as incombustible white ash, coal is constituted of carbon,
hydrogen, oxygen, nitrogen, and a little sulphur. All the varied and interesting
products obtained by the destructive distillation of coal are combinations
of two or more of these four or five elements. Illuminating gas
is far from being the only product when coal is heated without access of
air; for of the numerous substances volatized at the red heat of the gas-retort
a great number are not only incapable of affording light, but liable
to generate noxious compounds when burnt. Besides this there are numerous
bodies which, though leaving the retort in the gaseous form, immediately
assume the liquid or solid state at ordinary temperatures. All such
substances must be separated before permanent gases are obtained fit for
illuminating purposes and capable of being carried through pipes to distant
places. Thus an important part of the apparatus for gas manufacture
consists in arrangements for separating the condensable bodies, and for
removing useless or injurious gases from the remainder.
Fig. 347.—Section of Gas-making Apparatus.
The products resulting from the destructive distillation of the coal may,
therefore, be classified as—a, solids left behind in the retort; b, solids and
liquids condensed by cooling the vapours which issue from the retort; c,
coal-gas—a mixture of gases from which certain useless and noxious constituents
must be removed. Fig. 347 is intended to give a diagrammatic
view of the apparatus employed in the generation, purification, and storage
of gas, the various parts being shown in section. A is the furnace containing
several retorts, of which B is one. From each retort a tube, d, rises
vertically, and curving downward like an inverted U, it enters a long horizontal
cylinder, f; half filled with water, beneath the surface of which the
open end of the recurved tube dips. The cylinder containing water passes
horizontally along the whole range of furnaces in the gas-works, and is
known as the hydraulic main. It is here, then, the tar and the moisture
first condense, and the pipe is always kept half full of these liquids, so that
the ends of the pipes, d, from the retorts, dipping beneath its surface, form
766traps or water-valves, which allow any retort to be opened without permitting
the gas to escape. As the tar accumulates in the hydraulic main,
it flows over through a pipe, g, leading downwards into the tar-well, H.
The gases take the same course; but while the tar flows down the vertical
tube, R, the gases pass on through j into the condensers or refrigerators.
Gas cannot escape from the open end of the tube, for it is always closed by
the liquids—tar and ammoniacal liquor—which accumulate and flow over
the top of the open inner vessel into the cistern, S, from which they are
drawn off from time to time by the stop-cock, I. Although when the gas
has arrived at this cistern much of its tar and ammoniacal vapours have
been condensed, a portion is still retained by reason of the high temperature
of the gas; and this has to be removed before it is permitted to enter
the purifier. This is the object of passing the gas through the series of
pipes, j j, forming the condenser. These are kept cool by the large surface
they expose to the air, and, when necessary, cold water from the cistern,
K, may be made to flow over them. The tar and other liquids condense
in the iron chest, T, which is so divided by partitions as to compel the gas
to pass through the whole series of tubes; and as the liquid accumulates,
it also overflows into the tar-well. The cooled gas then enters the purifier,
L L, in which are layers of slaked lime placed on a number of shelves. By
contact with the extensive surface of slaked lime the gas has its sulphuretted
hydrogen, carbonic acid, and some other impurities, removed; and
it then, through the tube n, enters the gasholder, in which it is stored up
for use.
Hydrated oxide of iron is now much used for purifying coal-gas. The
oxide is mixed with sawdust, and placed in layers 10 in. thick. Sulphide
of iron and water is formed; and when the mixture has ceased to absorb
any more, it is removed and exposed to a current of air; the hydrated
oxide is thus reproduced and sulphur set free. The process may be repeated
many times in succession, until the absorbent power is impaired by
the accumulation of sulphur.
The gasholder—or “gasometer,” as it is often improperly named—is an
immense cylindrical bell, made of wrought iron plates, and inverted in a tank
of water, in which it rises or falls. It is counterpoised by weights attached
to chains passing over pulleys, so as to press the gas with a small force in
order to drive it along the main, which communicates with the pipes supplying
it to the various consumers. The pressure impelling the gas through
the mains does not in general exceed that of a column of water two or
three inches high.
It will be necessary, after this slight outline describing the essential
parts of the apparatus, to enter more fully into the details of the several
parts.
The retorts are constructed of wrought iron, cast iron, or earthenware,
and in shape are cylindrical, with a diameter of 12 in. to 18 in., or more,
and a length of 6 ft. to 10 ft. Though sometimes circular in section, other
forms are commonly used—such as the elliptical, and especially the ⌓-shaped.
The retorts are closed except at the mouth-end, Fig. 348, from the
top of which rises the stand-pipe, A, which has usually a diameter of about
5 in. When the charge has been introduced, the mouth is closed by a
plate of iron, B, closely and securely applied by means of a screw, C, as shown
in the figure—a perfectly tight joint being obtained by a luting of lime mortar
spread on the part of the lid which comes into contact with the mouth of
the retort. The retorts are always set horizontally in the furnace—each
767furnace usually including a set of five retorts. The charge of coals is introduced
on a tray of sheet iron adapted to the size of the retort, which,
when properly pushed in, is inverted so as turn out the contents, and then
withdrawn.
The time required to completely expel the volatile constituents from the
charge in a gas retort varies very much, because there are great diversities
in the composition of the different kinds of coal employed. Some varieties
of coal, such as cannel, are easily decomposed, and the operation may be
complete in about three hours; while other kinds may require double that
time. The quantity of gas procurable from a given weight of coal also varies
according to the kind of coal made use of. Thus, while a hundredweight
of cannel may give 430 cubic feet
of gas, the same weight of Newcastle
coals will yield but 370 cubic
feet. The nature of the gases
given off from a retort will be
different at the different stages
of the operation.
The scene presented by the
retort-house of a large gas manufactory,
when viewed at night, is
a singular spectacle. The strange
lurid gleams which shoot out
amid the general darkness as the
retorts are opened to withdraw
the coke, and the black forms
of the workmen partially illuminated
by the glare, or flitting like
dark shadows across it, form a
picture which might engage the
pencil of a Rembrandt. In Fig.
348a is depicted the retort-house
at the Imperial Gas Works, King’s
Cross. Here the retorts are arranged
in several tiers—the coal
being brought, and the coke withdrawn,
by the aid of an iron carriage
running on rails parallel to
the line of furnaces.
Fig. 348.—The Retort.
In the process of heating, a proper regulation of the temperature is of
the highest importance. It is found that when the retorts are heated to
bright cherry-red, the best results are obtained. At a lower temperature
a larger quantity of condensable vapours are given off, which collect in the
gasholders and distributing pipes as solid or liquid, and occasion much
inconvenience, while the quantity of gas obtained is decreased. On the
other hand, if the temperature be too high, some of the gases are decomposed,
and the quantity of carbon contained in the product is so much
diminished as seriously to impair the illuminating power. Again, every
second the gases after their production remain in the red-hot retort diminishes
their light-giving value; for those hydro-carbons on which the
luminiferous power of the gas depends, are then liable to partial decomposition;
a portion of their carbon is deposited on the walls of the retort
in a dense layer, gradually choking it up, while the liberated hydrogen does
769not add to the illuminating but to the heating constituents of the gas. A
plan has been patented by Mr. White, of Manchester, for rapidly removing
the illuminating gases from the retort by sweeping them out by means of
a current of what has been termed “water gas.” This water gas is produced
by causing steam to pass over heated coke, and is a mixture of carbonic
acid, carbonic oxide, and hydrogen. Though only two of these are
combustible gases—and even they do not yield light by their combustion,
and, by adding to the bulk of the gas, serve rather to dilute it—yet it has
been found that in some cases twice the amount of light is obtainable by
White’s process than the same weight of coal supplies when treated in the
ordinary manner.
Fig. 348a.—Retort House of the Imperial Gas-Works, King’s Cross, London.
The hydraulic main, as already mentioned, being kept half full of tar
into which the lower ends of the dip-pipes descend, prevents the gas from
escaping through the stand-pipes when the lid of a retort is removed for
the introduction of a fresh charge. The hydraulic main is from 12 to 18
in. diameter, and the dip pipes pass into it by gas-tight joints. Various
forms of purifiers are in use besides the simple one already mentioned.
Some of these have arrangements for agitating the gas with a purifying
liquid by mechanical means, the motion being supplied by a steam engine.
The gasholder, as it sinks in the water of the cistern, presses with less
force on the contained gas, and unless this inequality of pressure were
counteracted there would be very unequal velocities in the flow of gas
from the burner. The equality of pressure is obtained by making the
weight of the chains by which the gasholder is suspended equal to half
the weight the gasholder loses in the same length of its motion. Gasholders
are also constructed without chains or counterpoises, as these are
found to be unnecessary where the height of the gasholder does not exceed
half its width. In such cases, especially when the vessel is very large, the
difference of pressure at the highest and lowest position is quite inconsiderable,
and nothing more is necessary than that upright guides or pillars
be placed to preserve the vertical motion of the vessel. Another improvement,
which enables a lofty gasholder to be used without increasing the
depth of the tank, consists in forming the gasholder of several cylinders,
which slide in and out of one another like the draw-tubes of a telescope.
Each cylinder has a groove formed by turning up the iron inside the rim,
and at the top of the next cylinder the edge is turned outwards so as to drop
in the groove or channel, which thus forms a gas-tight joint, for it is of
course filled with water as it rises. The pressure is, however, more accurately
regulated by an apparatus called the governor, through which the
gas passes in before it enters the mains. The construction and action of
the regulator will be understood from Fig. 349, where A represents a kind
of miniature gasholder, inverted in the cistern, B. From the centre of the
interior of the bell hangs a cone, C, within the contracted orifice of the
inlet-pipe. If this cone be drawn up, the size of the orifice, D, is reduced,
and, on the other hand, by its descent it enlarges the opening through
which the gas passes outward. By properly adjusting the weights of the
counterpoise, E, such a position of the cone may be found that the gas passes
into the mains at an assigned pressure. Suppose, now, that from any
cause the pressure of gas in F increases, that pressure acting upon the
inverted bell, A, causes it to rise and carry with it the cone, which, by
narrowing the orifice of the outlet, checks the flow of gas. Similarly, a
decrease of pressure in the mains would be followed by the descent of the
cone, and consequently freer egress of gas. In hilly towns it is necessary
770to fix regulators of this kind at certain heights in order to equalize the
pressure. It is found that a difference of 30 ft. in level affects the pressure
of gas in the same main to about the same amount as would a column
of water one-fifth of an inch high, the pressure being least at the lowest
point.
Fig. 349.—The Gas Governor.
Coal-gas is a mixture of several gases, and these may be classified as,
first, the light-giving gases, or those which burn with a luminous flame;
secondly, gases which burn with a non-luminous flame, and which therefore
contribute to the heat, and not to the light, of a gas-flame, and have
the effect of diluting the gas; third, gases and vapours which are properly
termed impurities, as they are either incombustible or by their combustion
give rise to injurious products. Of the first kind the principal is olefiant
gas, a gas which burns with a brilliant white flame without smoke. It is
a compound of hydrogen and carbon, six parts by weight of carbon being
combined with one part by weight of hydrogen. Besides olefiant gas other
gaseous hydro-carbons are found in smaller quantities. These contain a
larger proportion of carbon than olefiant gas. The second class contains
hydrogen, light carburetted hydrogen, and carbonic oxide. Hydrogen is
one element of water, of which it forms one-ninth of the weight. It burns
with a flame giving singularly little light, but having intensely heating
power; in fact, one of the brightest lights we can produce is obtained by
allowing the flame of burning hydrogen to heat a piece of lime. Light
carburetted hydrogen, like olefiant gas, is a compound of hydrogen and
carbon, but the proportion of carbon to hydrogen is only half what it is in
olefiant gas, namely, three parts to one. This gas enters largely into the
771composition of coal-gas, and occurs naturally in the coal seams, being, in
fact, the dreaded fire-damp of the miner. It is much lighter than olefiant
gas, for while that gas is of nearly the same specific gravity as atmospheric
air, light carburetted hydrogen is only a little more than half that specific
gravity. It is this ingredient of coal-gas which renders it so light as to be
available for inflating balloons. It burns with either a bluish or a slightly
yellow flame, yielding hardly any light. Olefiant gas and the other luminiferous
hydro-carbons, when exposed to a bright red heat, split up for the
most part into this gas and carbon. This explains the importance of rapidly
removing the gas from the retort in which it is generated, a point which
has been referred to above. Carbonic oxide is a gas which one may often
see burning with a pale blue flame above the glowing embers of a common
fire, the flame giving, however, little light. It is a compound of carbon and
oxygen, containing only one-half the quantity of oxygen which its carbon
is capable of uniting with, and therefore ready to unite with another proportion,
which it does in burning, carbonic acid being the product.
The third class of constituents of coal-gas—the impurities—are those
which the manufacturer strives to remove by passing the gas over lime,
milk of lime, oxide of iron, &c. Sulphuretted hydrogen, a compound of
sulphur and hydrogen, has an extremely nauseous odour resembling that
of rotten eggs. It is always formed in the distillation of coal, and if not
removed from the gas in the process of purification, it has a very objectionable
effect; for one product of its combustion is sulphurous acid, and in a
room where such gas is burnt much damage may be done by the acid
vapours; for example, the bindings of books, &c., soon become deteriorated
from this cause. The detection of sulphuretted hydrogen in coal-gas is
quite easy, for it is only necessary to hold in a current of the gas a piece
of paper dipped in a solution of the acetate of lead. If in a few minutes
the paper becomes discoloured the presence of sulphuretted hydrogen is
indicated.
But the bête noire of the gas-maker is a substance called “sulphide of
carbon,” which is formed whenever sulphur and carbonaceous matters are
brought together at an elevated temperature. Sulphide of carbon is, in
the pure state, a colourless liquid, of an intensely offensive odour, resembling
the disagreeable effluvia of putrefying cabbages. The liquid is extremely
volatile, and coal-gas usually contains some of its vapour. When
too high a temperature is used in the generation of the gas, it contains
a large quantity of this deleterious ingredient, especially if the amount of
sulphur contained in the coal is at all considerable. This sulphide of
carbon vapour is very inflammable, and one product of its combustion is
a large quantity of sulphurous acid. This substance cannot be removed
from coal-gas by any process sufficiently cheap to admit of its application
on the large scale. It is said, however, that by passing the gas over a
solution of potash in methylated spirit, the sulphide of carbon vapour can
be completely got rid of. The price of these materials renders the process
available in special cases only, where the damage done by the sulphurous
acid would be serious, as in libraries, &c. Besides the impurities we have
already enumerated, many others are present in greater or less quantity.
Carbonic acid—the gas resulting from the complete combustion of carbon—should
be entirely removed by the lime purifiers, as the presence of even
a small percentage detracts materially from the illuminating power. This
gas is not inflammable and cannot support combustion. It has decided
acid properties, and readily unites with alkaline bases forming carbonates:
772it is upon this behaviour that its removal by lime depends. The illuminating
power of coal-gas containing only 1 per cent. of carbonic acid is
reduced thereby by about one-fifteenth of its whole amount.
The proper mode of burning the gas so as to obtain the maximum
amount of light it is capable of yielding requires a compliance with certain
physical and chemical conditions. The artificial production of light depends
upon the fact that by sufficiently heating any substance, it becomes
luminous, and the higher the temperature the greater the luminosity. The
light emitted by solid bodies moderately heated is at first red in colour; as
the temperature rises it becomes yellow, which gradually changes to white
when the heat becomes very intense. The widest difference exists, however,
in the temperature required to render solids or liquids luminous, and
that needed to cause gases to give off light. In all luminous flames the
light is emitted by solid particles highly heated. Every luminous gas-flame
contains solid particles of carbon, as may be easily shown by the
soot deposited on any cold body—such as a piece of metal—introduced into
the flame. On the other hand, the flame of burning hydrogen, which produces
only aqueous vapour, furnishes no light, but a heat so intense, that
a piece of lime introduced into the jet becomes luminous to a degree hardly
supportable by the eye. The conditions requisite, therefore, for burning
illuminating gas are, first, just such a supply of air as will prevent particles
of carbon from escaping unconsumed in the form of smoke, and yet not
enough to burn up the carbon before it has separated from the hydrogen,
and passed through the flame in the solid state; second, the attainment of
the highest possible temperature in the flame, compatible with the former
condition. When the supply of oxygen is not in excess, the hydrogen of
the gaseous hydro-carbon appears to burn first; the carbon is set free, and
its solid particles immersed in the flame of the burning hydrogen are there
intensely heated; but ultimately reaching the outer part of the flame, they
enter into combination with the oxygen of the air, producing carbonic acid;
or if present in excessive quantity, they are thrown off as smoke. If the purpose
of burning the gas is to obtain heating effects only, this is accomplished
by supplying air in such quantities, that the carbon enters into combination
with oxygen in the body of the flame, without
a previous separation from the hydrogen
with which it is combined. In this
case a higher temperature is attained, and
the flame is wholly free from smoke; so that
vessels of any kind placed over it remain
perfectly clean and free from the least deposit
of soot. The last result is of great advantage
in chemical processes, especially
where glass vessels require to be heated,
for the chemist retains an uninterrupted
view of the actions taking place in his
flasks and retorts.
Fig. 350.—Bunsen’s Burner.
No better illustration of the nature of
the combustion in a gas-flame can be found
than is furnished by Bunsen’s burner, Fig.
350, now universally employed as a source
of heat in chemical laboratories. In this
burner the gas issues from a small orifice at the level of a, near the bottom of
the tube, b, which is open at the top, and is in free communication at the bottom
773with openings through which air enters and mixes with the gas, as they
rise together in the tube and are ignited at the top. If the pressure of the
gas be properly regulated, the flame does not descend in the tube, but the
mixture burns at the top of the tube, producing a pale blue flame incapable
of emitting light, but much hotter than an ordinary flame, for the combustion
is much quicker. If the openings at a be stopped, the supply of air
to the interior of the tube is cut off, and then the gas burns at the top of
the tube, b, in the ordinary manner, giving a luminous flame. Ordinary
gas-jets burning in the streets, at open stalls or shops, may be seen on a
windy night to have their light almost extinguished by the increased
supply of oxygen, carried mechanically into the body of the flame, the
white light instantly changing to pale blue. The disappearance of the
light in such cases is due, as in Bunsen’s burner, to the supply of oxygen
in sufficient quantity to combine at once with the carbon as well as the
hydrogen of the hydro-carbons.
Fig. 351.—Faraday’s Ventilating Gas-burner.
The burners now chiefly used for the consumption of coal-gas for illuminating
purposes are the bat’s-wing, the fish-tail, and various forms of
Argand. The bat’s-wing burner is simply a fine slit cut in an iron nipple,
and it produces a flat fan-like flame. The fish-tail is formed by boring
two holes so that two jets of gas inclined at an angle of about 60° infringe
on each other and produce a flat sheet of flame. The Argand, in its
simplest form, consists of a tubular ring perforated with a number of small
holes from which the gas issues. Many modifications of this kind of
burner have been devised, in all of which a glass chimney is requisite to
obtain a current of air sufficient to consume the gas without smoke, and
it is important that the height of the chimney should be adapted to the
amount of light required if the gas is to be used economically. Argand
774burners are specially advantageous where a concentrated light is required.
Fig. 351 represents a ventilating gas-burner, contrived by Faraday, the
object being to remove from the apartment the whole of the products of
the combustion of the gas. A is the pipe conveying the gas to the
Argand burner, B, the flame of which is enclosed in the usual cylindrical
glass chimney, C C, open at the top. This is enclosed in a wider glass
cylinder closed at the top by a double disc of talc, D D, and opening at its
base into the ventilating tube, E E. The direction of the currents produced
by the heat of the flame is shown by the arrows. The whole is entirely
enclosed by a globe of ground glass. Means are provided for regulating
the draught in the pipe, E E, which, when heated, creates of itself a strong
current of air through the apparatus.
The illuminating power of coal-gas may be measured directly by comparing
the intensity of the light emitted by a gas-flame consuming a known
quantity of gas per hour with the light yielded by some standard source.
The standard usually employed is a spermaceti candle burning at the rate
of 120 grains of sperm per hour. It is not necessary that the candle actually
used should consume exactly this amount, but the consumption of
sperm by the candle during the course of each experiment is ascertained
by the loss of weight, and the results obtained are easily reduced to the
standard of 120 grains per hour. An instrument is used for determining
the relative intensities of the illumination, called Bunsen’s photometer. It
consists of a graduated rule, or bar of wood or metal, about 10 ft. long. At
one end of this bar is placed the standard candle, at the other is the gas-flame.
A stand slides along the rule supporting a circular paper screen at
the level of the two flames, and at right angles to the line joining them.
This paper screen is made of thin writing-paper, which has been brushed
over with a solution of spermaceti, except a spot in the centre, or, more
simply, a grease-spot is made in the middle of a piece of paper. In consequence
the paper surrounding the spot is much more transparent; yet when
it is placed so that both sides are equally illuminated, a spectator will not
perceive the spot in the centre when viewing the screen on either side.
When the screen has been placed by trial in such a position between the
two sources of light, it is only necessary to measure its distance from each
flame in order to compute the number of times the illuminating power of
the gas-flame exceeds that of the candle. This computation is based on
the fact that the intensity of the light from any source diminishes as the
square of the distance from the source. Thus, if a sheet of paper be illuminated
by a candle at 2 ft. distance, it will receive only one-fourth of the
light that would fall upon it were its distance but 1 ft., and if removed to
3 ft. distance it has only one-ninth of the light. In the instrument used
for measuring the illuminating power of gas the rule is graduated in accordance
with this law, so that the relative intensities may be read off at once.
The gas passes through a meter for measuring accurately the quantity per
minute which is consumed by the burner, and there is also a gauge for
ascertaining the pressure. Another mode of estimating the illuminating
power of coal-gas is by determining the quantity of carbon contained in a
given volume. For, in general, the richness of the gas in carbon is a fair
index of the quantity of its luminiferous constituents. This may be readily
effected by exploding the gas with oxygen, and measuring the amount of
carbonic acid produced. Still more accurate determinations of the illuminating
value of gas may be obtained by a detailed chemical analysis.
The illuminating power of any gas is so calculated that it represents the
775number of times that the light emitted by a jet of the gas, burning at the
rate of 5 cubic feet per hour, exceeds the light given off by the standard
sperm candle burning 120 grains of sperm per hour. For example, when
it is said that the illuminating power of London gas is 13, it is meant that
when the gas is burnt in an ordinary burner at the rate of 5 cubic feet per
hour, the light is equal to that given by thirteen sperm candles burning
together 13 × 120 grains per hour. The quality of gas varies very much,
as it depends upon the kind of coal employed, and upon the mode in which
the manufacture is conducted. The following are the results of experiments
made to determine the illuminating power of the gas supplied to
several large towns:
Candles.
London
12·1
Paris
12·3
Birmingham
15·0
Berlin
15·5
Carlisle
16·0
Liverpool
22·0
Manchester
22·0
Glasgow
28·0
The relative quantities of tar, ammonia water, and coke yielded in various
gas manufactories also vary very considerably for the same reasons.
In the early days of gas illumination the consumers were charged according
to the number of burners; but this arrangement proved so unsatisfactory
that the gas-meter became a necessity, and already in 1817 meters had
been devised, which were not essentially different from those now in use.
Although gas is used in so many houses, there are few persons who have
any notion of the mechanism of the gas-meter. Our space will not allow
full details of the construction, but the following particulars may be mentioned.
In the ordinary “wet” meter there is a drum divided into four
compartments by radiating partitions; this drum revolves on a horizontal
axis, and the lower half of the drum, or rather more, is beneath the surface
of water contained in the case, the water being at the same level inside and
outside the drum. The gas enters one of the closed chambers formed
between the surface of the water and a partition of the drum. Its pressure
tends to increase the size of the chamber, hence the drum revolves. The
preceding division of the drum being filled with gas, this is driven into the
exit pipe by the motion of the drum, as it is included in a space comprised
between the water and a partition. Each division in turn comes into communication
with the gas-main, and as it is filled passes on towards the position
in which a passage is opened for it to the exit-pipe. Each turn of the
drum, therefore, carries forward a definite quantity of gas, and the only
thing necessary is a train of wheels, to register the number of revolutions
made by the drum. The “wet” meter is much inferior in almost every
respect to the “dry” meter, in which no water is used. The principle of the
“dry” meter is very simple. The gas pours into an expanding chamber,
partly constructed of a flexible material, and which may be compared to
the bellows of a circular accordion. The expansion is made to compress
another similar chamber, already filled with gas, which is thus forced
through the exit-pipe. When the first chamber has expanded to a definite
volume, it moves a lever, and this reverses the communications. The expanded
chamber is now opened to the exit-pipe, and the other to the
entrance-pipe, and so on alternately. A train of wheels registers the number
of movements on a set of dials.
Recent years have brought no essential changes in the methods of gas
making, although of course improvements in many minor details of the
776processes and of the apparatus have been effected. These demand no
description at our hands, as they are of interest only to those concerned
with the actual technology of gas-making, nor need some of the later
forms of burners for using the gas be noticed, as these are sufficiently
familiar. They really do effect a considerable economy in the consumption
of gas, especially in cases where a more powerful light is required.
But the reader will have already learnt from a foregoing section on
Electric Lighting that the importance of gas as an illuminant is already
on the wane. Indeed, it will not be too much to say that, before the close
of the present century, every town will have its streets, and still more certainly,
all its places of public assembly, such as theatres, concert halls,
churches, libraries, &c., fitted with installations for electric illumination,
and even in shops and private houses, it is probable that before long, gas
will be superseded by the electric light. Some of the disadvantages of
burning gas have already been referred to, and the danger attending its
accidental escape into apartments is illustrated by the yearly tale of victims
to suffocation and violent explosions. The inherent disadvantage of gas
used as an illuminant, is the enormous quantity of heat produced by its
combustion, compared with the amount of light evolved. The absolute
quantity of heat required to render a body highly luminous is really very
small, for masses of matter almost inappreciable become very luminous,
provided only that their temperature be sufficiently raised. Thus, for
example, the few residual particles of gas in a Geissler’s tube (p. 431)
become incandescent by electrical discharges, while the number of them is
too small to sensibly heat the glass vessel, and the very attenuated carbon
filament in an electric glow lamp suffices by the mere contraction and
concentration of the current within it raising its temperature high enough,
to diffuse a brighter light than a large gas-flame. This explains the fact
alluded to elsewhere, that if instead of burning the gas we use it in a
gas engine, driving a dynamo connected with an electric light installation,
we shall obtain a much greater luminous effect. As there is no combustion,
the surrounding air is neither heated nor deteriorated with gaseous
products and smoke.
Without any rivalry from the electric-light, gas, as a domestic luminant,
has now met with a competitor on the ground of cheapness in the mineral
oils mentioned in the preceding article. If these could be deprived of
their unpleasant odour, and a perfectly safe lamp contrived for burning
them, it would be only under very favourable conditions that gas could
compete with them on the score of economy. But of late years two applications
of gas to other purposes than to illumination will have been
observed. First to heating, for warming, cooking, and other domestic
purposes, and also in various processes in the arts. In all the appliances
so used, the principle of Bunsen’s burner (p. 722) is adopted, and stoves,
fireplaces, and kitchen-ranges, heated by gas have obvious advantages
in their greater cleanliness and readiness. The other new application of
gas is as a motive power in the gas engine, by which a very convenient
supply of mechanical energy is afforded. There can be little doubt that
in the future, gas will be greatly used for these purposes, and perhaps be
for them consumed as largely as at present. A singular thing in the
history of gas-manufacture is the great value that the bye-products have
attained, that is to say, the ammoniacal liquor, the coke, and especially
the tar. So many valuable substances are now derived from this last, that
even if coal should cease to be destructively distilled for gas, the operation
would still be largely carried on if only for the tar.
777A jet of hydrogen gas burning in a dark room is all but invisible, yet
no gas can give so intense a heat. The lime-light, which no doubt is
perfectly familiar to everyone as an illuminant in magic lantern projections,
is simply a jet of mixed hydrogen and oxygen gases directed on a
piece of lime, which is rendered incandescent by the heat. The flame
of the Bunsen burner (p. 772) is distinguishable only by a very pale blue
colour, and it is impossible to discern objects, or to read by its light in an
otherwise dark room. But if a piece of thin platinum wire formed into
a coil, as by twisting round a pencil, be introduced into the flame, the
wire will glow with great brilliancy, and its thickness will seem much increased.
It will, in fact, emit so much light that reading by its glow
becomes easy. This shows that, as already stated, a solid will give off
light at a temperature which scarcely suffices to make a gas visible.
Thus a Bunsen burner flame can be made to give light simply by putting
into it some incombustible solid, which itself incapable or suffering any
chemical change under the conditions, nevertheless becomes luminous by
merely acquiring the temperature of the almost invisible heated gas.
The cause of the luminosity of the ordinary gas burner, as compared
with the almost invisible Bunsen burner flame, has, indeed, been already
explained on a previous page, but the phenomenon is again, by the experiment
just referred to, brought clearly before our attention; and it
becomes obvious that substances other than the carbon of the hydro-carbon
constituents of the coal gas will emit rays of light. Chemical
analysis shows that by far the larger proportion of the constituents of
ordinary coal-gas consist of gases which do not themselves produce
luminous flames, and that, taking 16 candle-gas, about 10 candles of the
illuminating power is due to compounds of which the gas does not contain
more than 4 per cent. Nearly half the bulk of purified coal-gas is
hydrogen, which itself gives no light whatever when burnt; marsh-gas,
which burns with only a slight luminosity, forms 35 per cent. of ordinary
coal-gas; and there is usually present about 7 per cent. of carbonic oxide,
which in burning gives only a pale blue flame. This shows that by far
the greatest product of the combustion of coal-gas is not light but heat.
The flame of hydrogen is much the hottest known, and as that gas enters
so largely into the composition of coal-gas, and the complete combustion
of all the other constituents takes place when the gas is previously mixed
with air, as in the Bunsen burner, we are provided with an economical
means of obtaining high temperatures. But coal-gas was in the first instance
intended to provide us with a cheap illuminant, and although for
some time the gas itself was very impure, and it was long before the
crude appliances for burning it were superseded by contrivances giving
steadier and more brilliant lights, such as the Argand and the regenerative
burners. It is only quite recently that the full illuminating possibilities
of coal-gas have been developed by the happy notion of converting
the heating power of its flame into light-giving power, by the simple plan
of suspending a suitable solid over the hot but non-luminous Bunsen
burner.
The manner in which an effective method of doing this was discovered
is not a little curious. The construction of the ordinary incandescent
electric lamp, Fig. 280h, involves the necessity of enclosing the carbon
filament in an exhausted glass bulb; and it was when Auer von Welsbach
was engaged in attempting to find some substance that could be brought
into incandescence by the electric current, and yet be incombustible even
778in the open air, that his investigations led to the invention we have now
to describe—an invention apparently destined to give a new lease of life
to coal-gas illumination.
Fig. 351a.
Fig. 351b.
It is singular also that Welsbach, in seeking for the most suitable
materials for heating to incandescence in the Bunsen burner flame,
should find them in certain very rare minerals, containing a group of
elements formerly of interest only to the scientific chemist, and up to that
time devoid of any practical applications. The names of these elements,
the oxides of which are called “earths,” will, of course, be strange to
non-chemical readers, but we give their names, with the remark that the
nearest familiar substance they at all resemble is aluminium, of which
the oxide, or “earth,” is alumina. These rare metals, the oxides of which
779are the materials of the Welsbach “mantle,” are all discoveries of the
present century, or nearly so, and they are called lanthanum, zirconium,
thorium, cerium, didymium, yttrium, erbium, &c. They occur as silicates
or phosphates very sparingly, and in a few localities in Norway; but
some of them have now been found more abundantly in America. The
minerals, from which for the most part the oxides are obtained, are called
monazite, orthite, and thorite. It was found after many trials that a blend
of these earths in certain proportions gives a mantle that yields a pure
white light, while any preponderance of one or another would impart
some tint to the light. This proper blending of the constituents forms a
great improvement on the first mantles, which generally shed a greenish
light.
Fig. 351c.
Fig. 351d.
The mantles are made by an ingenious process, in which a network of
cotton thread is knitted into the form of a tube; this is cut up into suitable
lengths, and a piece attached to form the top. The network is then
saturated with a solution of the nitrates of the rare earths above-mentioned,
and dried on glass rods. After this a loop of asbestos thread
780is passed through the top, by which the mantle may be attached to its
support. The mantle is now shaped to the required form, and the cotton
thread burnt off, when a thin skeleton of the oxides is left reproducing
the form of the original network. The mantle is again strongly heated,
and after cooling is dipped into a solution of collodion, dried, and carefully
laid in a box. The collodion serves to strengthen the mantle sufficiently
for transit, for it is very frail, and would otherwise be liable to fall
in pieces by slight shocks. Fig. 351d is a full-sized representation of the
completed mantle, and Fig. 351e shows it mounted on the burner, where
a rather small flame is allowed for the first time to play upon it, by which
the collodion is quickly burnt off, and then the chimney-glass is placed
over it, as in Fig. 351a. In the earlier forms of lamp the lighting of the
gas was a matter requiring some delicacy of manipulation, for a rude
shock, or an awkward touch might cause the mantle to crumble into ruin,
but now the makers fit their lamps with a by-pass by which a very small
flame is maintained within the lamp ready to light up the gas when that
is fully turned on. (Fig. 351c.) The makers have also now made the
lamps available for street lighting, to which the fragility of the mantle
was formerly an obstacle, as it was liable to collapse by the tremor of the
traffic. This risk has been obviated by providing
a spring to support the mantle at the
base. (Fig. 351b.)
Fig. 351e.
The qualities of the Welsbach lamp have
been examined by competent persons, and
from the statements they supply, we extract
the following particulars. The light is, for
the same gas consumption, seven times that
of an ordinary gas burner; more than four
times that of an Argand burner; more than
twice that of a “regenerative” lamp. It
follows, of course, that, light for light, the
products of combustion, such as carbonic
acid, heat, &c., amount to only something
like ⅙th of those produced by ordinary
burners, and the consumption of the gas is
perfect, there being absolutely no smoke.
Though the mantles have to be renewed
about three times a year, when the burners
are in constant use, the total cost, light for
light, is only ¼th of that of ordinary burners.
The light of the Welsbach burner is whiter
than ordinary gaslight. It is rich in the blue
rays, and, therefore, more like daylight, permitting
well the comparison of shades of
colour, and it is excellently suited for workers
with the microscope, &c. This new gas-lighting must also be a great
boon to photographers using artificial illumination, for the actinic power
is, with the same visual illumination, nearly twice that of the ordinary
gas flame.
781
Fig. 352.—Apparatus for making Magenta.
COAL-TAR COLOURS.
Coal-tar is an exceedingly complex material, being a mixture of a
great number of different substances. The following table shows the
chemical name of many of the substances obtainable from the coal-tar. It
must not be supposed that these substances exist ready formed in the coal,
and that they are merely expelled by the heat. We can understand better
how heat, acting upon an apparently simple substance like coal, and one
containing so few elements, is able to produce so large a variety of different
bodies, if we remember that heat is the agent most often employed to effect
chemical changes, and that from even two elements, variously combined,
bodies differing entirely from each other are producible.
Substances found in Coal-Tar.
a.COMPOUNDS OF CARBON AND HYDROGEN.
Hydrides of amyl, hexyl, heptyl, nonyl, and decyl.
This list contains only the names of substances which have actually been
found in the coal-tar, and it is certain that a number of products must have
escaped notice. It is obvious, too, that by using coal of different kinds, and
by varying the temperature and pressure at which the operation of distilling
the coal is effected, we shall probably be able to increase the number
of possible constituents of coal-tar almost indefinitely. The list above presents
to the non-chemical reader a string of quite unfamiliar names; but,
though the system of nomenclature in chemistry is far from perfect, yet
each of these names has a meaning for the chemist beyond the mere designation
of a substance. The chemical name aims at showing, or at least
suggesting, the composition of a body and the general class to which it
belongs. This may be illustrated by the names of hydro-carbons in the
above list. The five compounds headed by benzol have many properties
in common, and each one is entirely different in its chemical behaviour to
those which follow amylene. The Greek numerals enter into the names of
the latter, in order to express, in this case, the number of atoms of carbon
which are supposed to be contained in each ultimate particle of the body.
We write down in parallel columns the names of these two classes of bodies,
together with the symbols which represent their composition, reminding the
reader that the letter C represents carbon; the letter alone indicating one
atom of that element, but, when followed by a small figure, it implies that
number of carbon atoms; in like manner H, N, and O represent atoms of
hydrogen, nitrogen, and oxygen respectively.
Hexylene
C6H12
Heptylene
C7H14
Octylene
C8H16
Nonylene
C9H18
Decylene
C10H20
Benzol
C6H6
Toluol
C7H8
Xylol
C8H10
Cumol
C9H12
Cymol
C10H14
If these lists be carefully examined, it will be observed that there is a
regular progression in the constituent atoms, so that each set of substances
forms a series, the differences being always the same. The various bodies
contained in the coal-tar are separated from each other by taking advantage
of the fact that each substance has its own boiling-point; that is, there
is a certain temperature, different for each body, at which it will rise into
vapour quickly and continuously. Benzol, for example, boils at 82° C.,
toluol at 114° C., and phenol at 188° C.; so that, if we apply heat to a mixture
of these three substances, the benzol will boil when the temperature
reaches 82°, and will pass away in vapour, carrying off heat, so that the
temperature will not rise until all the benzol has been driven off; then, when
the temperature reaches 114°, the toluol will begin to come off, but not
783until that has all passed over into the receiver will the temperature rise
above 114°; and the phenol remaining will distil only at 188°.
Another mode of separating bodies when mixed together is by treating
them with a liquid which acts on, or dissolves out, some of the constituents,
but not the rest. The coal-tar, as it is received from the gas-works, is
placed in large stills, capable, perhaps, of holding several thousand gallons,
and usually made of wrought iron. Stills sufficiently good for the purpose
are commonly constructed from the worn-out boilers of steam engines.
The application of heat, of course, causes the more volatile substances to
come over first. These are condensed and collected apart until products
begin to come off which are heavier than water. The first portion of the
distillate, containing the lighter liquids, is termed “coal naphtha.” The process
is continued, and heavier liquids come over, forming what is called in
the trade the “dead oil.” Pitch remains behind in the retort, from which
it is usually run out while hot, but sometimes the distillation is carried a
step further.
The chief colour-producing substances contained in coal-tar are benzol,
toluol, phenol, naphthalene, and anthracene. The aniline which is present
in the tar is very small in amount, and if this ready-formed aniline were
our only supply, it would be impossible to make colours from it on an
industrial scale. The first of the above-named substances, benzol, was
discovered by Faraday, in 1825, in liquid produced by strongly compressing
gas obtained from oil. He called it bicarburet of hydrogen; but afterwards
another chemist, having procured the same body by distilling benzoic acid
with lime, termed it benzine. It readily dissolves fats and oils; and is used
domestically for removing grease-spots, cleaning gloves, &c., and in the arts
as a solvent of india-rubber and gutta-percha. It is a very limpid, colourless
liquid, very volatile, and, when pure, is of a peculiar but not disagreeable
odour. It boils at 82° C., and, cooled to the freezing-point of water, it
solidifies into beautiful transparent crystals, a property which is sometimes
taken advantage of to separate it in a state of purity from other liquids
which do not so solidify.
Benzol is very inflammable, and its vapour produces an explosive mixture
with air. The vapour, which is invisible, will run out of any leak in
the apparatus, like water, and flow along the ground. Accidents have
occurred from this cause, and a case is on record in which the vapour
having crept along the floor of the works, was set on fire by a furnace
forty feet away from the apparatus, the flame, of course, running back to
the spot from which the vapour was issuing. Benzol is a dreadful substance
for spreading fire should it become ignited, for, being lighter than
water, it floats upon its surface, and therefore the flames cannot be extinguished
in the ordinary way. The discovery of the presence of benzol in
coal-tar was made by Hofman in 1845. It is obtained from the light oil of
coal-tar by first purifying this liquid by alternately distilling it with steam
and treating with sulphuric acid several times. The product so obtained
is a colourless liquid, sold as “rectified coal naphtha,” which, however, has
again to be several times re-distilled with a careful regulation of the temperature,
so that the benzol may be distilled off from other substances, boiling
at a somewhat higher temperature, with which it is mixed. Even then
the resulting liquid (commercial benzol) contains notable quantities of
toluol. If benzol be added in small quantities at a time to very strong and
warm nitric acid, a brisk action takes place, and when after some time water
is added, a yellow oily-looking liquid falls to the bottom of the vessel. The
784benzol will have disappeared, for nitric acid under such circumstances acts
upon it by taking out of each particle an atom of hydrogen, which it replaces
by a group of atoms of nitrogen and oxygen, and, instead of benzol,
we have the yellow oil, nitro-benzol. Chemists are accustomed to represent
actions of this kind by what is called a chemical equation, the left-hand
side showing the symbols representing the constitution of the bodies which
are placed together, and the right hand the symbols of the bodies which
result from the chemical action. Here is the equation representing the
action we have described:
C6H6
+
NO2OH
=
C6H5(NO2)
+
HOH
Benzol.
Nitric acid.
Nitro-benzol.
Water.
Fig. 353.—Iron Pots for making Nitro-Benzol.
Fig. 354.—Section of Apparatus for making Nitro-Benzol.
Nitro-benzol has a sweet taste and a fragrant odour. It is known in
commerce under the names of artificial oil of bitter almonds and essence
of mirbane, and it has been used for perfuming soap. The chemical action
between benzol and concentrated nitric acid is so violent that, when nitro-benzol
first had to be manufactured on the large scale, great difficulty was
experienced on account of the serious explosions which occurred. The
apparatus now used in making nitro-benzol on the large scale is represented
785in Fig. 353, which shows some of the cast-iron pots, of which there is usually
a long row. These pots are about 4½ ft. in diameter, and the same in
depth. Each is provided with a stirrer, which is made to revolve by a
bevil-wheel, c, on its spindle, working with a pinion on a shaft, b, driven by a
steam engine. A layer of water is kept on the tops of the lids, the water
being constantly passed in and drawn off through the pipes, d, in order
to keep it cool. For the chemical action is, as usual, attended with heat,
which vaporizes some of the benzol, but the cold lid re-condenses the
vapour, which would otherwise escape with the nitrous fumes that pass off
by the pipe, a. There is at e an opening, through which the material may
be introduced, and in the bottom of the vessel is an aperture through which
the products may be drawn off. Fig. 354 shows a section of one of the
cast-iron vessels, and exhibits the mode in which the spindle of the stirrer
passes through the lid. In the cup, a, filled with a liquid, a kind of inverted
cup, which is attached to the spindle, turns round freely. It would
not do to choose water for the liquid in this cup, for water would, by absorbing
the nitrous fumes, form an acid capable of attacking and destroying
the spindle. Nothing has been found to answer better for this purpose than
nitro-benzol itself. The charge introduced into these vessels is a mixture
786of nitric and sulphuric acids together with the benzol. During the action,
which may last twelve or fourteen days, no heat is applied, for the mixture
becomes hot spontaneously, and in fact care must be taken that it does
not become too hot. The nitro-benzol thus obtained is purified by washing
with water and solution of soda.
Fig. 355.—Apparatus for making Aniline.
If nitro-benzol were brought into contact with ordinary hydrogen gas, no
action whatever would take place. But it is well known to chemists that
gases which are just being liberated from a compound have at the instant
of their generation much more powerful chemical properties than they possess
afterwards. Gases in this condition are said to be in the nascent state.
787If we submit nitro-benzol to the action of nascent hydrogen we find a
remarkable change is produced. This change consists, first, in the hydrogen
robbing the nitro-benzol of all its oxygen atoms; second, in the addition
of hydrogen to the remainder; third, in some re-arrangement of the
atoms, by which a new body is formed. Not that these changes are successive,
or that we actually know the movement of atoms, but we are thus
able to form ideas which correspond with the final result. The new substance
is named aniline. It is regarded by chemists as a base; that is,
a substance capable of neutralizing and combining with an acid to form a
salt. Its composition is represented by the symbols C6H5 H2N. Aniline
was found in coal-tar in 1834, and even its colour-producing power was
noticed, for its discoverer named it kyanol, in allusion to the blue colour
it produced with chloride of lime. Later it was obtained by distilling indigo
with potash, and hence received its present name from anil, the Portuguese
for indigo. The quantity of aniline contained in the tar is quite
insignificant.
Aniline is prepared from nitro-benzol on the large scale by heating it
with acetic acid and iron filings or iron borings, a process which rapidly
changes the nitro-benzol into aniline. The equation representing the
change is—
C6H5NO2
+
H6
=
C6H5H2N
+
2H2O.
Nitro-benzol.
Hydrogen.
Aniline.
Water.
The operation is effected in the apparatus represented in Fig. 355. It
consists of a large iron cylinder, within which works a paddle on a vertical
revolving spindle, which, being hollow, is also a pipe to convey high pressure
steam within the apparatus.
Fig. 356 is a section of the hollow
spindle, in which f is the pivot at
the bottom of the cylinder on
which it turns; d is the stirring
paddle; e is an aperture admitting
the steam from the pipe, c, forming
the shaft of the paddle, which
is made to revolve by the bevil-wheel.
The steams enters by the
elbow-pipe, which has a nozzle
ground to fit the head of the vertical
revolving pipe, upon which
it is pressed down by the screw.
When the materials have been
introduced into the cylinder, the
stirrer is set in motion, and superheated
steam is sent down the
pipe; the aniline is volatilized and
passes with the steam through the
pipe, which is connected with a worm surrounded by cold water. The aniline
is purified by another distillation over lime or soda. When pure, aniline
is a colourless, somewhat oily-looking liquid, of a feeble aromatic odour.
Under the influence of light and air it becomes of a brownish tint, in which
condition it usually presents itself in commerce. It scarcely dissolves in
water, but is readily soluble in alcohol, ether, &c.
Fig. 356.—Section of Hollow Spindle,—Aniline Apparatus.
It was Mr. Perkin who, in 1856, first obtained from aniline a substance
788practically available for dyeing. Let it be noticed that when Mr. Perkin
discovered aniline purple, he was not engaged in searching for dye-stuffs,
but was carrying on a purely scientific investigation as to the possibility of
artificially preparing quinine. With this view, having selected a substance
into the composition of which nitrogen, hydrogen, and carbon enter in
exactly the same proportions as they occur in quinine, but differing from it
by containing no oxygen, he thought it not improbable that by oxidizing
this body he might obtain quinine. In this he was disappointed, for the
result was a dirty reddish-brown powder. Being desirous, however, of
understanding more fully the nature of this reddish powder, he proceeded
to try the effects of oxidation on other similarly constituted but more
simple bodies. For this purpose he fortunately selected aniline, which,
when treated with sulphuric acid and bichromate of potash, he found to
yield a perfectly black product. Persevering in his experiments by examining
this black substance, he obtained, by digesting it with spirits of wine,
the now well-known “aniline purple.” Mr. Perkin, having determined to
make the aniline purple on the large scale, patented his process, and succeeded
in overcoming the many obstacles incident to the establishment of
a new manufacture requiring as its raw material products not at that time
met with as commercial articles. The process is now carried on the
large scale by mixing sulphuric acid and aniline in the proportions in which
they combine to form the sulphate of aniline, and dissolving by boiling with
water in a large vat. Bichromate of potash is dissolved in water in another
large vat. When both solutions are cold, they are mixed together in a
still larger vessel and allowed to stand a day or two. A fine black powder
settles on the bottom of the vessel in large quantities; this is collected
in filters, washed with water, and dried. This powder is not aniline purple
alone, but a mixture of this with other products, presenting a very unpromising
appearance; but when it has been digested for some time with
diluted methylated spirit, all the colouring matter is dissolved out, and is
obtained from the solution by placing the latter in a still, where the spirit
is distilled off and collected for future use, while all the colouring matter
remains behind, held in solution by the water. From this aqueous solution
the mauve is thrown down by adding caustic soda. It is collected, washed,
and drained until of a pasty consistence, in which condition it is sent into the
market. It can be obtained in crystals, but the commercial article is seldom
required in this form, as the additional expense is not compensated by any
superiority in the practical applications of the colour. Mauve is readily
soluble in spirits of wine, but not very soluble in water. Its tinctorial power
is so great that one-tenth of a grain suffices to impart quite a deep colour
to a gallon of water. Silk and woollen fabrics have an extraordinary
attraction for this colouring matter, which attaches itself very firmly to their
fibres. If some white wool is dipped into even a very dilute solution, the
colour is quickly absorbed. Mauve is more permanent than any other coal-tar
colour, being little affected by the prolonged action of light.
Mauve is chemically a salt of a base which has been termed “mauveine.”
Mauveine itself is a nearly black crystalline powder, which forms
solutions of a dull blue-violet tint, but when an acid is added to such a
solution the tint is at once changed to purple. Mauveine is a powerful
base, displacing ammonia from its compounds. The commercial crystallized
mauve is the acetate of mauveine.
The process by which Mr. Perkin originally obtained mauve from aniline
evidently depends upon the well-known oxidizing property of bichromate
789of potash, and experiments were accordingly made with other, oxidizing
bodies and aniline; in fact, patents were taken out for the use of nearly
every known oxidizing chemical. Three years after Mr. Perkin’s discovery
of mauve, M. Verguin, of Lyons, obtained, by treating crude aniline with
chloride of tin, the bright red colouring matter now known as magenta.
It was found also that crude aniline, when treated with other metallic
chlorides, nitrates, or other salts, which are oxidizing agents less powerful
than bichromate of potash, yields this bright red colouring matter. A
process patented by Medlock, in 1860, in which arsenic acid is the oxidizing
agent, has almost entirely superseded, in England at least, all the
others yet proposed for the manufacture of magenta. It is not a little
remarkable that magenta would not have been discovered had M. Verguin
and others operated on pure aniline instead of on the ordinary commercial
article. For it was found subsequently by Dr. Hofman that pure aniline cannot
be made to yield magenta: the presence of another body is necessary.
A reference to the table of coal-tar constituents will show that there is
a hydro-carbon named “toluol.” This substance is of a similar nature to
benzol, and has a boiling-point so little above that of benzol, that in the
rough methods of separation usually employed, a notable quantity of toluol
is carried over with the benzol, and is always present in the commercial
article. In the processes which benzol undergoes for conversion into aniline,
the toluol accompanies it in a series of parallel transformations, resulting
in the production of a base termed “toluidine”—similar to aniline—being,
however, in its pure state a solid at ordinary temperatures. We
write down the symbols representing the composition of the bodies formed
in the two cases in order to clearly show this:
Benzol
C6H6
Nitro-benzol
C6H5(NO2)
Aniline
C6H5NH2
Toluol
C7H8
Nitro-toluol
C7H7(NO2)
Toluidine
C7H7NH2
This aniline prepared from commercial benzol always contains some
toluidine; and it is essential for the production of magenta that this substance
should be operated on along with the aniline. Whether the presence
of some toluidine is also necessary for the production of mauve and other
colours is not yet known, but they are always prepared from commercial
benzol. It is certain that pure aniline yields no magenta, neither does pure
toluidine; but a mixture supplies it in abundance. For the preparation of
magenta the best proportions for this mixture would be about three parts
of aniline to one of toluidine; but, in practice, it is not necessary to obtain
the two substances separately, as benzol, mixed with a sufficient quantity
of toluol, may be obtained by regulating the distillation. The apparatus
used in the production of magenta is shown in Fig. 352. It consists of a
large iron pot set over a furnace in brickwork, and having a lid with a stuffing-box,
through which passes a spindle carrying a stirrer. A bent tube rises
from the lid, and is connected with a worm surrounded by cold water, for
the purpose of condensing the aniline which is vapourized in the process.
The aniline, containing a due amount of toluidine, is mixed in this apparatus
with about one and a half times its weight of a saturated solution of arsenic
acid (H3AsO4). The fire is lighted and kept up for several hours: water
first, and lastly aniline, distil over. When the operation is ended, steam is
blown through the apparatus, thus carrying off an additional portion of
aniline. The crude product is then boiled with water, the solution filtered,
790and common salt added, which precipitates an impure magenta. This is
afterwards dissolved and recrystallized several times. The crystals of this
magenta—like those of many of the coal-colour products—have a peculiar
greenish metallic lustre; they dissolve in warm water, forming a deep
purplish-red solution. The chemical composition of magenta has been investigated
by Dr. Hofman, who found it to be a salt of an organic base,
to which he gave the name of “rosaniline.” This rosaniline is easily obtained
from magenta by addition to its solution of an alkali. While all its
salts are intensely coloured, rosaniline itself is a perfectly colourless substance,
becoming reddened by exposure to the air, as it absorbs carbonic
acid, thus passing to the condition of a salt. Rosaniline, then, displays
its chromatic powers only when it is combined with an acid. This property
is sometimes shown at lectures in a striking manner by dipping a
piece of paper into a colourless solution of rosaniline, and exposing it to
the air, when, as the rosaniline absorbs carbonic acid, the paper changes
from white to red. A more elegant form of the same experiment is to dip
a white rose into a solution of rosaniline containing a little ammonia. As
the ammonia escapes, or is expelled by a current of warm air, the same
kind of action occurs, and the white rose changes to red—as if by magic,
the emblem of the House of York is transformed into the badge of Lancaster!
The chemical nature of rosaniline is regarded as analogous to
that of ammonia—it is, in fact, looked upon by chemists as a sort of ammonia,
in each particle of which some atoms of hydrogen have been replaced
by certain groups of carbon and hydrogen atoms—some of these groups being
derived from the aniline and others from the toluidine. The particular
salt of rosaniline which constitutes the crude product of the action on the
aniline and toluidine, depends on the substance employed to effect the
oxidation. If a chloride, the resulting product is chloride of rosaniline; if
a nitrate, it is the nitrate; and so on. The magenta which is formed in the
first instance by the process we have described is an arseniate of rosaniline;
but in the subsequent processes, it is converted into the chloride—the
salt usually sold as magenta. Other salts of rosaniline are made on
the large scale—especially the acetate, the beautiful crystals of which have
the advantage of being very soluble.
Magenta attaches itself strongly to animal fibres, but the colour is somewhat
fugacious under the action of sunlight. It is used not only as a dye,
but more largely as the raw material from which a number of other beautiful
colours are obtained. For this reason it is manufactured on an enormous
scale, thousands of tons being produced annually, and the money value of
the colour produced from it must be reckoned by thousands of pounds.
Yet aniline was a few years ago merely a curiosity never met with out of
the laboratory of the scientific chemist. It is stated that a single firm now
makes more than twelve tons of aniline weekly, and on its premises may
be seen tanks, in each of which 30,000 gallons of magenta solution is
depositing its crystals. If a salt of rosaniline be heated with aniline, the
colour changes gradually through purple to blue, while ammonia is at the
same time given off. This is the colour known as aniline blue, “bleu du
Lyons,” &c. In its preparation it has been found that the best results are
obtained by employing the salt of some weak acid—acetate of rosaniline,
for example—and pure aniline, that is, aniline free from toluidine. The
operation is conducted in iron pots very similar to those used in making
magenta, but smaller. These pots are not set over a fire, but a number of
them are placed in a large vessel containing oil, by which they can be
791maintained at a regulated temperature when the oil is heated. The crude
product undergoes several purifications, and the aniline blue is supplied
in commerce in powder, or dissolved in spirits of wine. It is insoluble in
water, and this has been an obstacle to its employment; but recently a
similar substance has been obtained in a soluble form, and is extensively
used for dyeing wool, under the name of “Nicholson’s blue.” Other blues
have been similarly prepared, and from the same two substances, magenta
and aniline, a colour known as “violet imperial” was formerly made in
very large quantities, but it has been superseded by the colours about to
be described. It may be well to mention that these blues and violets have
been found to contain bases formed of rosaniline, in which one, two, or
three atoms of hydrogen are replaced by the group C6H5. This group
of atoms will be noticed to belong to aniline, and chemists have named
it phenyl, and, therefore, bases of these coloured salts are respectively
named phenyl-rosaniline, di-phenyl-rosaniline, tri-phenyl-rosaniline. But
Dr. Hofman found that other groups of atoms besides C6H5 may be made
to take the place of H in rosaniline. By acting on rosaniline or its salts
with iodides of ethyl, C2H5I, or iodide of methyl, CH3I, he obtained a
beautiful series of violets, of which many shades could be produced, varying
from red-purple to blue. These are the colours so well known as
Hofman’s violets, and are prepared on the large scale by heating a solution
of magenta (chloride of rosaniline) in alcohol or wood spirit, with the
iodide of ethyl or the iodide of methyl. The nature and proportions of
the ingredients are regulated according to the tint required. The vessels
are hermetically closed during the heating, which is accomplished by steam
admitted into a steam-jacket surrounding the vessel. The crude product
has to be separated from the substances with which it is mixed, and the
colouring matter is finally obtained, presenting in the solid state the
peculiar semi-metallic lustre so characteristic of these products. Like the
other colours, Hofman’s violets are salts of colourless bases, which, as
indicated above, are substitution products of rosaniline. The tints they
produce incline to red, violet, or blue, according as one, two, or three
hydrogen atoms are replaced by the ethyl or methyl groups. Colours have
also been obtained from mauve and iodide of ethyl—for example, the
dye known in commerce as “dahlia.” Other colours are procured from
magenta by treating it with various compounds: one such is the “Britannia
violet,” discovered also by Mr. Perkin, who procures it from magenta
and a hydrocarbon-bromide derived from the action of bromine or common
turpentine. This is a very useful colour, and is largely used in dyeing and
printing violets, of which any shades may be obtained.
Another derivative of rosaniline is the aniline green. It is obtained by
dissolving the rosaniline salt in dilute sulphuric acid, adding crude aldehyde
(a substance obtained by acting with oxidizing agents on alcohol).
The mixture is heated until a sample dissolves in acidulated water with a
blue tint; it is poured out into boiling water containing in solution hyposulphite
of sodium, boiled, the liquid filtered; and the green dye, if required
in the solid state, is precipitated by carbonate of sodium. Aniline green
dyes wool and silk, the latter especially, of a magnificent green; perhaps as
beautiful a colour as any of the coal-tar series, and one which has the singular
advantage among greens of looking as beautiful in artificial light as
in daylight. The manner in which this dye was discovered is somewhat
curious. It is related by Mr. Perkin of a dyer, named Chirpin, that he was
trying to render permanent a blue colouring matter, which had been found
792could be produced from rosaniline by the action of aldehyde and sulphuric
acid. After a number of fruitless attempts at fixing it, he confided his
perplexities to a photographic friend, who evidently thought that if it was
possible to fix a photograph, anything else might be fixed in like manner,
for he recommended his confidant to try hyposulphite of sodium. On
making the experiment, however, the dyer did not succeed in fixing his
blue, but converted it into the splendid aldehyde green. Like other colouring
matters we have described, this is a salt of a colourless base containing
sulphur. Like rosaniline, the colourless base takes on the characteristic
colour of its salts by merely absorbing carbonic acid from the air.
Again, by a modification of the process for producing the Hofman violets,
another green of an entirely different constitution may be obtained. It is
bluer in tint than the former, and is much used for cotton and silks, under
the name of “iodine green.”
In the manufacture of magenta there is formed a residuum or bye-product,
consisting of a resinous, feebly basic substance, from which Nicholson obtained
a dye, imparting to silk and wool a gorgeous golden yellow colour.
This dye cannot be obtained directly, but is always produced in greater or
less quantity when magenta is made on the large scale, and is separated
during the purification. By first dyeing the silk or wool with magenta, and
then with this dye, which is commercially known as “phosphine,” brilliant
scarlet tints are obtained. The yellow colours have been found to be salts
of a base termed chrysaniline, a sort of chemical relative of rosaniline, as
may be seen in comparing the formulæ which represent their constitution,
with which we place also the symbol for another substance obtained by
submitting rosaniline to the influence of nascent hydrogen. This body,
leucaniline, again yields rosaniline very readily when the hydrogen is removed
by oxidizing agents. It will be noticed that the three bodies form
a series the members of which differ only by H2, thus indicating their close
relationship.
C20H17N3
Chrysaniline.
C20H19N3
Rosaniline.
C20H21N3
Leucaniline.
Some idea will have been obtained from the foregoing particulars of
the great colour-supplying capabilities of aniline; but we have not yet
exhausted the utility of this interesting substance. It is probable that the
letters on the page now under the reader’s eye owe their blackness to an
aniline product. For after all the salts furnishing the lovely tints we have
mentioned have been extracted, there is in their manufacture a final
residuum, and from this an intense black is obtained, which is largely used
in the manufacture of printing-ink.
We have mentioned phenol as a substance yielding colours. Phenol is
the body now so well known as a disinfectant under the name of “carbolic
acid,” a name given to it by its discoverer, Runge, who prepared it from
coal-tar, in 1834. Phenol forms colourless crystals, which dissolve to some
extent in water, and very readily in alcohol. It is a powerful antiseptic,
that is, it arrests the process of putrefaction in animal or vegetable bodies,
and it is also highly poisonous. The constitution of phenol is given by
the formula C6H5 OH, in which the reader will recognize the same group
of atoms already indicated as entering into the aniline derivatives. From
some of these phenol may in fact be obtained, and although it cannot be
formed directly from benzol, phenol can be made to furnish benzol. When
793crude phenol is treated with a sulphuric acid and oxalic acid, a substance
is obtained which presents itself as a brittle resinous mass of a brown
colour, with greenish metallic lustre. This substance is called rosolic acid
by chemists, but in commerce it is known as aurine, and is used for dyeing
silk of an orange colour, which, however, is not very permanent. But by
heating rosolic acid with liquid ammonia, a permanent red dye is procured
which has been termed peonine, and has been much used for woollen goods.
But it lately had the reputation of exerting a poisonous action, producing
blistering and sores when stockings or other articles dyed with it were
worn in contact with the skin. It is now, therefore, less extensively employed.
Coralline, another body identical with or very similar to the
former, is similarly prepared from rosolic acid by heating it with ammonia
under pressure.
Again, by heating coralline with aniline, a blue dye, known as “azurine,”
or “azuline,” was formerly made in large quantities; but it has been supplanted
by the aniline blues already described.
When phenol is acted upon by nitric acid new compounds are produced,
standing in the same relation to phenol as nitro-benzol does to benzol. The
final result of the action of nitric acid on phenol is picric acid, called also
“carbazotic acid,” and, more systematically, “tri-nitro-phenol;” for it is
regarded as phenol in which three of the hydrogen atoms have been replaced
by the group NO2 thus, C6H2(NO2)3 OH. It forms bright yellow-coloured
crystals, and its solution readily imparts a bright pure yellow
colour to wool, silk, &c. It received the name of picric acid (πικρος, bitter)
from the exceedingly bitter taste of even an extremely diluted solution. It
is said that picric acid is employed as an adulterant in bitter ale instead of
hops. Now, the colouring power of picric acid is so great, that even the
minute quantity which could be used to impart bitterness to beer is recognizable
by dipping a piece of white wool into the beer, when, if picric acid
be present, the wool acquires a clear yellow tint. Besides its employment
as a yellow, it is useful for procuring green tints by combination with the
blues. Picric acid again furnishes, by treatment with cyanide of potassium, a
deep red colour, consisting of an acid which, when combined with ammonia,
furnishes a magnificent colouring material—which is, in fact, murexide, a
dye identical with the famous Tyrian purple of the ancients, and formerly
obtainable only from certain kinds of shell-fish.
Naphthaline—another of the colour-yielding substances of coal-tar—is,
like benzol, a hydro-carbon, but one belonging to quite another chemical
series. Its formula is C10H8, and it has an interest to chemists altogether
apart from its industrial uses, from having been the subject of the classic
researches of the French chemist, Laurent—researches which resulted
in the introduction of new and fertile ideas into chemical science, contributing
largely to its rapid progress. Naphthaline forms colourless
crystals, which, like camphor, slowly volatilize at ordinary temperatures,
and are readily distilled in a current of steam. It is thus sufficiently volatile
to escape complete deposition in the condensers of the gas-works, and
to be partly carried over into the mains, where its collection occasions
some trouble. Nitric acid acts upon naphthaline in a manner analogous
to that in which it acts on benzol, forming nitro-naphthaline, which, in its
turn, submitted to the action of iron filings and acetic acid, is transformed
into a base called “naphthylamine.” The salts of naphthylamine are
coloured products which, in some cases, have been found available as dyes.
There is a crimson colour, and a yellow largely used under the name of
794“Manchester yellow,” for imparting to silk and wool a gorgeous golden
yellow colour. Another coloured derivative of naphthaline, called “carminaphtha,”
was discovered by Laurent in the course of his researches.
It would be easy to fill this volume with descriptions of the properties,
and modes of preparing the numerous colouring matters that have been
obtained from coal-tar products. In order to give the reader an idea of
the extent to which the tar products have been made to minister to our
sense of the beautiful, a list is here given of the principal colouring matters
from these sources that have been employed in the arts. The various
names under which a product has been commercially known are in most
cases given. It must be understood that the same name is frequently
applied to products chemically distinct, and some of the names which
appear as synonyms may also in reality indicate different substances.
Aniline blue, rosaniline blue, Hofman’s blue, bleu de Paris, bleu de Lyons, bleu de Mulhouse, bleu de Mexique, bleu de nuit, bleu lumière, night blue.
Hofman’s blue.
Nicholson’s blue, soluble blue.
Hofman’s violet, rosaniline violet.
A long series of red and blue violets, bearing Hofman’s name and distinguished in commerce by adding R or B, according to the redness or the blueness of the tint, ranging from RRRR to BBBB.
Dahlia.
Toluidine blue.
Violet de Paris.
Mauvaniline.
Violaniline.
Regina blue, opal blue, bleu de Fayolle, violet de Mulhouse.
Britannia violet.
Violet imperial.
And many others.
Reds.
Aniline red, new red, magenta, solferino, aniline, rougé, roseine, azaline.
Iodine green, iodide of methyl green, iodide of ethyl green.
Perkin’s green.
Browns.
Havanna brown.
Bismarck brown, aniline brown, Napoleon brown, aniline maroon.
Greys and Blacks.
Aniline grey, argentine.
Argentine black.
II.—Colours derived from Phenol.
Blues and Violets.
Isopurpuric acid, Grénat.
Azuline, azurine.
Reds.
Picramic acid.
Coralline, peonine.
Red coralline.
Yellows.
Picric acid, carbazotic acid.
Aurine, rosolic acid.
Green.
Chloropicrin.
Browns.
Picrate of ammonia.
Isopurpurate of potash.
Phenyl brown, phenicine.
III.—Colours derived from Naphthalene.
Reds.
Pseudoalizarine, naphthalic red.
Roseonaphthaline, carminaphtha.
Yellows.
Binitronaphthaline, naphthaline yellow, golden yellow, Manchester yellow.
And others.
The introduction of aniline colours into dyeing and calico-printing has
caused quite a revolution in these arts, the processes having become much
more simple, and the facilities for obtaining every variety of tint largely
increased. The arts of lithography, type-printing, paper-staining, &c.,
have also profited by the coal-tar colours. For such purposes the colour
796is prepared by fixing it on alumina, a process in which much difficulty
was at first experienced, for the colours are themselves almost all of a
basic nature. The desired result is now attained by fixing them on the
alumina with tannic or benzoic acid. These lakes produce brilliant printing-inks,
which are extensively used. The aniline colours are also employed
for coloured writing-inks, tinted soaps, imitations of bronzed surfaces, and
for a variety of other purposes.
Not many years ago coal-tar was a valueless substance: it was actually
given away by gas-makers to any one who chose to fetch it from the
works. It was then “matter in the wrong place;” but Mr. Perkin’s discovery
led to its being put in the right place, and it has become the raw
material of a manufacture creating an absolutely new industry, which has
developed with amazing rapidity. This industry dates from only 1856,
and in 1862 the annual value of its products was more than £400,000.
Dr. Hofman, in reporting on the coal-tar colours shown at the Paris Exhibition
of 1867, computed the value at that time at about £1,250,000, although
the products were much cheaper than before. Large manufactories
have been established in Great Britain, in France, Germany, Switzerland,
America, and other countries. The possibility of such an industry is an
interesting illustration of the manner in which the progress made in any
one branch of practical science may lead to unexpected developments in
other quarters. The quantity of aniline obtained from coal-tar is very
small compared to the amount of coal used, as may be seen from the
following table, in which the respective weights of the various products
required in the manufacture of mauve are arranged as given by Mr.
Perkin for the produce of 100 lbs. of coal.
lbs.
oz.
Coal
100
0
Coal-tar
10
12
Coal-tar naphtha
0
8½
Benzol
0
2¾
Nitro-benzol
0
4¼
Aniline
0
2¼
Mauve
0
0¼
From this we may perceive that had not the manufacture of gas been
greatly extended, so as to yield a large aggregate produce of tar, the requisite
supply for the manufacture of aniline would not have been attainable;
and the industrial application of the previously worthless bye-product
reacts upon gas manufacture by cheapening the price of that commodity,
thus tending still more to extend its use.
Although anthracene has already been named as one of the colour-producing
substances found in coal-tar, we have not in the list of coal-tar
colours included the colouring matter which anthracene is capable of yielding.
The reason is that this case stands apart in some respects from the
rest. The colours derived from aniline and the other substances already
enumerated are instances of the production of bodies not found in nature—mauve,
magenta, &c., do not, so far as we know, exist in nature. Their
artificial formation was a production of substances absolutely new. The
colour of which we have now to treat is, on the other hand, found in nature,
and from its occurrence in the rubia tinctoria, the roots of that plant have
for ages been employed as a source of colour, and are well known in this
country as “madder.” The plant is grown largely in Holland, in France,
797in the Levant, and in the south of Russia.[18] Madder is used in enormous
quantities for dyeing reds and purples: the well-known “Turkey red” is
due to the colouring matter of this root. The total annual value of the
madder grown is calculated to reach nearly 2½ million pounds sterling.
More than forty years ago it was discovered that the madder-root yielded
a colouring substance, to which the name of “alizarine” was bestowed, from
alizari, the commercial designation of madder in the Levant. The alizarine
does not exist in the fresh root, but is produced in the ordinary processes
of preparing the root and dyeing with it, in consequence of a peculiar
decomposition or fermentation. Alizarine may be procured from dried
madder by simply submitting it to sublimation, when beautiful orange
needle-shaped crystals of alizarine may be obtained. It is nearly insoluble
in water, but readily dissolves in hot spirits of wine. Acids do not dissolve
it, but potash dissolves it freely, striking a beautiful colour; with lime,
barytes, and oxide of iron, it forms purple lake, and with alumina a beautiful
red lake. According to Dr. Schunck, of Manchester, to whose investigations
we are indebted for much of our knowledge of madder, the root
contains a bitter uncrystallizable substance called “rubian,” which, under
the action of certain ferments, and of acids and alkalies, is decomposed
into a kind of sugar, and into alizarine and other colouring matters. The
ferment, which in the process of extracting the colouring matter from the
roots causes the formation of alizarine, is contained in the root itself.
18. The natural Order to which the madder plant belongs is interesting from the number of its
members which supply us with useful products. That valuable medicine, quinine, is obtained
from plants belonging to this family, as is also ipecacuanha, and other articles of the materia
medica. Coffea arabica, which furnishes the coffee-berry, is another member.
We have already seen how an investigation relating to a question of
pure chemical science accidentally led Mr. Perkin to the discovery of
mauve—the precursor of the long range of beautiful colours already described.
The mode of artificially preparing alizarine, so far from being an
accidental discovery, was sought for and found in 1869 by two German
chemists, Graebe and Liebermann. The researches of these chemists were
conducted in a highly scientific spirit. Instead of making attempts to produce
alizarine by trying various processes on first one body, then another,
to see if they could hit upon some tar product, or other substance, which
would yield the desired product, they began by operating analytically on
alizarine itself. Just as a mechanic ignorant of horology, required to make
a watch, would be more likely quickly to succeed in his task by taking a
watch to pieces to see how it is put together, than if he had tried all manner
of arranging springs and wheels until he hit upon the right way; so
these chemists set themselves to take alizarine to pieces, in order to see
from what materials they might be able to put it together. They decomposed
alizarine, and among the products found a hydro-carbon identical in
all its properties with anthracene.
Anthracene was discovered in coal-tar by Laurent in 1832, and its
properties were investigated by Anderson in 1862. It may be remarked
that such investigations were not conducted with a view to any industrial
uses of anthracene, but merely for the sake of chemistry as a science.
Certainly no one could have supposed at that time that the slightest relation
existed between anthracene and madder. Anthracene is a white
solid hydro-carbon, which comes over only in the last stages of the distillation
of coal-tar, accompanied by naphthaline, from which it is easily
separated by means of spirits of wine, by which the naphthaline is readily
798dissolved, but the anthracene scarcely. Anderson, in 1861, discovered,
among other results, that anthracene, C14H10, by treatment with nitric
acid became changed into oxy-anthracene, C14H8O2; and this reaction
we shall see is a step in the process of procuring alizarine from anthracene.
Phenol, as already mentioned, can be made to yield benzol, by a process
of deoxidization. With a view to similarly obtaining a hydro-carbon from
alizarine, Graebe and Liebermann passed its vapours over heated zinc
filings, and thus produced anthracene from alizarine. It now remained to
find a means of reversing this process, that is, so to act on anthracene as
to produce alizarine, and this was effected by treating anthracene with
bromine, forming a substance which, on fusing with caustic potash,
yielded alizarate of potash, from which pure alizarine resulted by treatment
with hydrochloric acid. A much cheaper method was, however,
necessary for manufacturing purposes, and it was found in a process by
which oxy-anthracene, C14O8H2, is treated at a high temperature with
strong sulphuric acid, and the product so formed heated with a strong
solution of potash, yielding alizarate of potassium as before. Many other
interesting substances appear to be formed in the reactions, but the nature
of these bodies has as yet been imperfectly investigated. No doubt whatever
can be entertained of the identity of natural with artificial alizarine;
and the production of this substance, the first instance of a natural colouring
matter made artificially, may be regarded as a great triumph of
chemical science. It was not long ago supposed that the chemical bodies
found in plants or animals, or produced by vital actions, could not possibly
be formed by any artificial process from their elements. The laws which
presided at their formation were, it was conceived, wholly different from
those which governed the chemicals of the laboratory, for they were held
to act exclusively under the influence of a mysterious agent, namely, “vital
force.” It was supposed, for example, that from pure carbon, oxygen, and
hydrogen, no chemist would ever be able to produce such a compound as
acetic acid. Accordingly the domain of chemical science, previous to the
end of the first quarter of the present century, was divided by an impassable
barrier into the two regions of organic and inorganic chemistry. Now,
however, the chemist is able to build up in his laboratory from their very
elements a great number of the so-called organic bodies. And it is quite
possible to do this in the case of alizarine; that is, a chemist having in
his laboratory the elements, hydrogen, carbon, oxygen, &c., could actually
build up the substance which gives its value to madder.
The quantity of anthracene procurable from coal-tar is, unfortunately,
comparatively small, for it is found that from the distillation of 2,000 tons
of coal only one ton of anthracene can be obtained. The use of artificial
alizarine would doubtless entirely supplant the employment of madder-root
if anthracene could be obtained in larger quantities; and the change
would be highly advantageous to this country, for as no madder is grown
in Great Britain, and we consume nearly half the whole annual growth, it
follows that every year a million pounds sterling go out of the country for
this commodity. When anthracene is produced from coal in sufficient
abundance, this sum will be available for the support of our own population.
In the meantime, the manufacture of artificial alizarine is restricted
only by the supply of its raw material.
The foregoing paragraphs of the present article, which were written for
the first edition of this work, not long after the introduction of artificial
alizarine, require some supplementary reference to the subsequent progress
799of discovery and to the increased importance of the manufacture of the
coal-tar colours on the large scale. Since the first introduction of alizarine
as a commercial product, the substance has received much attention from
chemists. The constitution of the body called above oxy-anthracene is
now better understood, and its chemical relationship is more clearly
indicated by the systematic name of anthraquinone, which it now bears.
The process of the manufacture of alizarine has received some advantageous
modifications, and the artificial product may now be said to have
entirely displaced the madder-root in dyeing. But, more than this,
chemists have found means of preparing a number of “derivatives” of
alizarine, many of which are either colouring matters or are easily converted
into such. Nearly thirty of these substances have been described,
and several of them have found extensive industrial applications. We
may mention alizarine blue, C17 H9 NO4, and another substance, produced
by combining that with sodium bi-sulphite, and having the formula
C17 H9 NO4 2Na H SO3. This last, manufactured largely, and sold
under the name of “alizarine blue S.,” is remarkable for being one of the
most permanent of all colouring matters. It is said to be a faster colour
than even indigo blue, which, indeed, it is rapidly replacing in dyeing,
where it is applicable to cotton with a chromium mordant and to silk with
one of alumina. Two other colouring matters have also been derived
from anthracene, and are much used in dyeing; one is commercially
named anthracene purple, the other is anthracene green, which supplies
the calico printer with very fast shades of olive-green.
Several of the substances enumerated in the list of coal-tar colours, in
pages 689 and 690, are now but little used, or altogether abandoned in
dyeing and calico printing, because either their beautiful hues prove too
fugitive, or other bodies of the same class can be produced at a much
cheaper rate. The range of choice is now of the amplest, for chemical
discovery has been wonderfully active, but in many cases the real nature
and relationship of the artificial colouring matters enumerated above have
only quite recently been made out. Mauve (now called rosaline), for
example, the oldest of all the colour-tar colours, and one which, as we
have seen, was manufactured on an extensive scale many years ago, is
now scarcely made at all, because much cheaper violets have taken its
place. The science of the tinctorial substances has lately taken a much
more distinct form, and this knowledge has borne fruit for industrial
purposes. It would be out of place here to review what has been done in
this way, but a few facts will show the richness of the field. It was only
in 1886 that the true chemical constitution of a class of coal-tar derivatives,
called azines, was first made out. They present themselves as pale
yellow or orange coloured crystallized solids, which melt at a comparatively
high temperature and may be distilled without decomposition.
Although highly coloured substances themselves, before they are converted
into fast dyes they require further treatment, which introduces into their
molecules another group of atoms. An almost indefinite number of such
compounds are theoretically possible, but from only a very few of them
many useful dye stuffs are now prepared on the large scale. Amongst
the most important of these are “neutral red,” “neutral violet,” and two
other violet colouring matters, “red dyestuff,” “fuchsia,” “giroflé,”
“Magdala red,” “indazine” and “Basle blue.”
Among the colouring matters before enumerated are “aniline yellow” and
“Bismarck brown.” Their real nature was not understood until a few years
800ago; and though the use of the aniline yellow itself has been abandoned
on account of its fugacity, the substance has been found a most prolific
parent, which has supplied dye stuffs of the most diverse and brilliant
hues. These form what chemists term the azo colours, and they have
been manufactured in great variety and on a very large scale. In 1876,
the class of them called chrysoidines was introduced, and again, in 1878,
tropœolines. Great numbers of different azo colours have been sent into
commerce under various names, such as “butter yellow,” “crocein scarlet,”
“Biebrich scarlet,” “Congo red,” “Bordeaux G.,” “fast red,” &c., &c.
About 140 of these azo dyes have been described, and the commercial
importance of this one class of compounds alone may be inferred from the
fact of no fewer than 200 patents having been taken out for processes
relating to their manufacture in the eleven years from 1878 to 1888.
It would not be difficult to fill this book with instances of the way in
which the resources of modern life have been increased by chemistry
alone, a science almost entirely the creation of the present century. Many
of the processes of manufacture in which chemistry is applied to the production
of articles of every-day use have been so often described, that
they may be assumed to be already so well known as to offer few elements
of novelty to the general reader, whose interest would also be likely to
flag if he were carried over a long range of even the brilliant discoveries
that are so delightful and instructive for the special students of this science.
There is no parallel to the rapidity of the progress made by the younger
branch of the science which concerns itself with the chemistry of one
element—namely, carbon and its various combinations, and it is from these
carbon compounds that our examples have been drawn. In the explosives,
we have some of these compounds supplying resistless forces for rending
rocks, and furnishing in warfare the most dreadful powers of destruction.
In anæsthetics, we see beneficent applications of others in alleviating
suffering and annulling pain; and again we have just shown how richly
another set of them can minister to our sense of beauty. The discussion
of these topics has afforded an opportunity for bringing before the reader
some of the laws or summarized statements of experimental facts, and
also some of those symbolical conceptions of the constitution of compounds,
which together furnish the clues that guide the chemist through the vast
labyrinth of the endless transformations of matter. The results attained
show that the notions expressed by such words as atom, molecule, compound
radical, structural formula, etc., have a true representative correspondence
with something in the actual constitution of bodies.
801
Fig. 357.—James Prescott Joule, F.R.S.
THE GREATEST DISCOVERY OF THE AGE.
The indulgent reader who may have followed the course of the foregoing
pages, will perhaps peruse the title of this article with some
little bewilderment. His attention has been drawn to one after another
of a series of remarkable and important discoveries, and he will naturally
wonder what can be the discovery which is greater than any of these.
Now, a discovery is great in proportion to the extent and importance of
the results that flow from it. These results may be immediate and practical,
as in the case of vaccination; or they may be scientific and intellectual, as
in Newton’s discovery of the identity of the force which draws a stone to
the ground with that which holds the planets in their orbits. Such discoveries
as most enlarge our knowledge of the world in which we live, by
embracing in simple laws a vast field of phenomena, are precisely those
which are most prolific in useful applications. If we admit, as we must,
the truth of Bacon’s aphorism, which declares that “Man, as the minister
and interpreter of nature, is limited in act and understanding by his observation
802of the order of nature; neither his understanding nor his power
extends farther,”[19] then it would be easy to show that the discovery of which
we have to treat, more than any other, must be of immense practical service
to mankind in every one of the ways in which a knowledge of the order of
nature can be of use, viz.:—“First, In showing in how to avoid attempting
impossibilities. Second, In securing us from important mistakes in attempting
what is, in itself, possible, by means either inadequate or actually
opposed to the end in view. Third, In enabling us to accomplish our
ends in the easiest, shortest, most economical, and most effectual manner.
Fourth, In inducing us to attempt, and enabling us to accomplish, objects
which, but for such knowledge, we should never have thought of undertaking.”[20]
19. “Homo naturæ minister et interpres, tantum facit et intelligit quantum de naturæ ordine re
vel mente observaverit: nec amplius scit aut potest.”—Novum Organum, Aphor. I.
A great principle, like that which we are about to explain to the reader,
is too vast in its bearings for its discovery and elaboration to have been
the work of an individual. This truth, and indeed the whole of our knowledge,
is but the result of the development and growth of pre-existing
knowledge. In fact, every discovery, however brilliant—every invention,
however ingenious, is but the expansion or improvement of an antecedent
discovery or invention. In strictness, therefore, it is impossible to say
where the first germ of even our newest notions may be found. Our latest
philosophy can be shown to be the result of progressive modifications of
ideas of remote ages. Hence every great truth, every grand invention,
has in reality been the offspring of many minds; but we record as the
discoverers and inventors those men who have made the longest strides
in the path of progress, and whose genius and labours have overcome
obstacles defying ordinary efforts.
The extent of the field which is covered by the principle we have in view
is so vast—embracing, as it does, the whole phenomena of the universe—that
it will not be possible to do more within our limits than give the reader
a general notion of the principle itself. It may be useful to instance a
truth which has a similar generality and significance, and which has also
acquired the force of an axiom, because it is verified every hour. It is
that greatest generalization of chemistry, affirming that in all its transformations
matter is indestructible, and can no more be destroyed than it can
be called into being at will. This truth is so well established, that some
philosophers have asserted that an opposite state of things is inconceivable.
But it was not always known; and there are at the present day untutored
minds which not only believe that a substance destroyed by fire is utterly
annihilated, but what they find inconceivable is the continued existence of
the substance in an invisible form. The candle burns away, its matter
vanishes from our view; but if we collect the invisible products of the combustion,
we find in them the whole substance of the candle in union with
the atmospheric oxygen. We may, in imagination, follow the indestructible
atoms of carbon in their migrations, from the atmosphere to the plant,
which is eaten by the animal and goes to form its fat, and from the tallow,
by combustion, back into the atmosphere again. The notion of the real
identity of matter under changing forms has been expressed by our great
dramatist in a well-known passage, which is remarkable for its philosophic
insight, when we consider the age in which it was written:
803Hamlet. To what base uses we may return, Horatio! Why may not imagination trace the
noble dust of Alexander, till he find it stopping a bung-hole?
Horatio. ‘Twere to consider too curiously to consider so.
Hamlet. No, faith, not a jot; but to follow him thither with modesty enough, and likelihood
to lead it. As thus: Alexander died, Alexander was buried, Alexander returneth to dust; the
dust is earth; of earth we make loam; and why of that loam, whereto he was converted, might
they not stop a beer-barrel?
Imperial Cæsar, dead, and turned to clay,
Might stop a hole to keep the wind away;
O, that the earth, which kept the world in awe,
Should patch a wall to expel the winter’s flaw!
Now the greatest discovery of our age is that force, like matter, is indestructible,
and that it can no more be created than can matter. The
reader may perhaps think the statement that we cannot create force is in
contradiction to experience. He will be disposed to ask, What is the steam
engine for but to create force? Do we not gain force by the pulley, the
lever, the hydraulic press? And are not tremendous forces produced when
we explode gunpowder or nitro-glycerine? When the principle with which
we are here concerned has been developed and stated in accurate terms, it
is hoped the reader will see the real nature of these contrivances. We are,
however, aware that it is quite impossible within the limits of a short article
to do much more than indicate a region of discovery abounding with results
which may be yet unfamiliar to some. Into this, if so minded, they should
seek for further guidance, which they will pleasantly find in the pages of
Dr. Tyndall’s “Heat considered as a Mode of Motion,” and in a little work
by Professor Balfour Stewart, entitled “The Conservation of Energy,” and
quite fascinating from the clearness and simplicity of its style. We may
continue our humble task of merely illustrating the general nature of this,
in reality the most important, subject which we have had occasion to bring
under the reader’s notice.
Perhaps the first step should be to point out the fact of the various
forces of nature—mechanical action, heat, light, electricity, magnetism,
chemical action—being so related that any one can be made to produce
all the rest directly or indirectly. Some examples of the conversion of
one form of force into another occur in the foregoing pages. Thus, on
page 485 an experiment is described in which electricity produces a mechanical
action; electricity is also shown, on page 496, to produce heat; on
page 491 chemical action; on page 501 magnetism. Then, as instances of
the inverse actions, there is on page 488, in the first paragraph on “Electric
Induction,” an account of the mode in which mechanical movements may
give rise to electricity; and in the experiments in pages 508, 509, and
particularly in the account of the Gramme machine, page 511, it is shown
how mechanical movements can, through magnetism, produce electricity.
The voltaic element, page 491, and the galvanic batteries, are instances of
chemical action supplying electricity. On page 518 a striking instance is
mentioned of changes in the forms of force. Every lighted candle is a
case of chemical action giving rise to light; and interesting examples of the
inverse relation are referred to on page 608. On page 168 is represented
the conversion of arrested motion into heat and light. We have, indeed,
sufficient examples to arrange a series of these conversions of forces in a
circle. Thus, chemical action (oxidation in the animal system) supplies
muscular power, this sets in motion a Gramme machine, the motion is converted
into electricity, the electricity produces the electric light, and light
causes chemical action, and with this the cycle is complete. In the steam
engine heat is converted into mechanical force, and many cases will present
804themselves to the reader’s mind in which mechanical actions give rise
to heat. The doctrine of a mutual dependence and convertibility among
all the forms of force was first definitively taught in England by Mr. (now
Justice) Grove, in 1842; and almost simultaneously Dr. Meyer promulgated
similar views in Germany. Mr. Grove subsequently embodied his doctrine
in a treatise, called “The Correlation of the Physical Forces,” which has
seen several editions.
But this teaching included much more than a mere connection between
the various forces, for it extended to quantitative relations. It declared
that a given amount of one force always produced a definite amount of
another, that a certain quantity of heat, for example, would give rise to
a certain amount of mechanical action, and that this amount of mechanical
action was the equivalent of the heat which produced it, and would in its turn
reproduce all that heat. These last doctrines, however, rested on a speculative
basis, until Mr. James Prescott Joule, of Manchester, carried out a most
patient, laborious, and elaborate experimental investigation of the subject.
His labours placed the truth of the numerical equivalence of forces on a
foundation which cannot be shaken; and he accomplished for the principle
of the indestructibility of force what Lavoisier did for that of the indestructibility
of matter—he established it on the incontrovertible basis of
accurate and conclusive experiment. His determination of the value of
the mechanical equivalent of heat especially is a model of experimental
research; and subsequent investigators have, by diversified methods, confirmed
the accuracy of his results. A great part of his work consisted in
finding what quantity of heat would be produced by a given quantity of
work.
Before we proceed to give an indication of one of Dr. Joule’s methods of
making this determination, we may point out that if a weight be raised a
certain height, the work which is done in raising it will be given out by the
weight in its descent. If you carry a 1 lb. weight to the top of the London
Monument, which is 200 ft. high, you perform 200 units of work. When the
weight is at the top, the work is not lost; for let the weight be attached
to a cord passing over a pulley, and it will, as it descends, draw up to the
top another 1 lb. weight.[21] If you drop the weight so that it falls freely, it
descends with a continually increasing velocity, strikes the pavement, and
comes to rest. Still your work is not lost. The collision of the weight and
the pavement develops heat, just as in the case of the experiment depicted
on page 168, but to a less degree—the increase of temperature might not
be sensible to the touch, but could be recognized by delicate instruments.
Your work, then, has now changed into the form of heat—the weight and
the pavement are hotter than before. This heat is carried off by contiguous
substances. But still your work is not lost, for it has made the earth
warmer. The heat, however, soon flows away by radiation from the earth,
and is diffused into space. The final result of your work is, then, that a
certain measurable quantity of heat has been sent off into space. Is your
work now finally lost? Not so: in reality, it is only diffused throughout
the universe in the form of radiant heat of low intensity. Yet it is lost for
ever for useful purposes; for from this final form of diffused heat there is
no known or conceivable process by which heat can be gathered up again.
Dr. Joule arranged paddles of brass or iron, so that they could turn freely
in a circular box containing water or quicksilver. From the sides of the
box partitions projected inwards, which contained openings that permitted
the divided arms of the paddle to pass, and preventing the liquid from
805moving en masse, thus caused a churning action when the paddle was
turned. Now, every one who has worked a rotatory churn knows that a
considerable resistance is offered to this action; but every one does not
know that under these circumstances the liquid becomes warmer. It was
Dr. Joule’s object to discover how much the temperature of his liquid was
raised by a measured quantity of work. He used very delicate thermometers,
and had to take a number of precautions which need not here be
described; and he obtained the definite quantity of work by the descent of
a known weight through a known distance, a cord attached to the weight
being wound on a drum, which communicated motion to the paddle. The
experiments were conducted with varying circumstances, to avoid chances
of error, and were repeated very many times until uniform and consistent
indications were always obtained. The result of the experiments showed
that 772 units of work (foot-pounds) furnished heat which would raise the
temperature of 1 lb. of water from 32° to 33° F., which is the unit of heat.
This number, 772, is a constant of the greatest importance in scientific and
practical calculations, and is called “the mechanical equivalent of heat.”
The amount of work it represents is sometimes called a “Joule,” and is
always represented in algebraical formulæ by “J.” Mr. Joule’s first paper
appeared in 1843, and soon afterwards various branches of the subject of
“The Equivalence and Persistence of Forces” were taken up by a number
of able men, who have advanced its principles along various lines of inquiry.
Among the most noted contributors to this question we find the names of
Sir William Thomson, Helmholtz, James Thomson, Rankin, Clausius,
Tait, Andrews, and Maxwell.
In the steam engine the case is the inverse of that presented by the above-named
experiment of Dr. Joule’s. Here we have heat producing work.
Now, the quantity of steam which enters the cylinder of a steam engine
may be found, and the temperature of the steam can be determined, and
from these the amount of heat which passes into the cylinder per minute,
say, can be calculated. A large portion of this heat is, in an ordinary
engine, yielded up to the condensing water, and another part is lost by
conduction and radiation from the cylinder, condenser, pipes, &c. But
both these quantities can be estimated. When the amount is compared
with that entering the cylinder in the steam, a difference is always found,
which leaves a quantity of heat unaccounted for. When this quantity is
compared with the work done by the engine in the same interval (which
work can be measured as described on page 10), it is always found that for
every 772 units of work a unit of heat has disappeared from the cylinder.
The numerical relation between work and heat which is established in
these two cases has been tested in many quite different ways; and, within
the limits of experimental errors, always with the same numerical result.
But equally definite quantitative relations are known to exist among all
the other forms of force; and the manner in which these are convertible
into each other has already been indicated, although want of space prevents
full illustration of this part of the subject. It may, however, be seen that
each form of force can be mediately or immediately converted into mechanical
effect, hence each is expressible in terms of work. That is to say, we
can assign to a unit of electricity, for example, a number expressing the
work which it would do if entirely converted into work; and the same
number also expresses the work which would be required to produce the
unit of electricity. An ounce of hydrogen in combining with 8 oz. of oxygen
produces a certain measurable quantity of heat. If that heat, say = H,
806were all converted into work, we now know that the work would = HJ.
Hence we can express a definite chemical action in terms of work. The
same is generally true of all physical forces, though in some cases, such as
light, vital action, &c., the quantitative relations have not yet been definitely
determined.
Since, then, all the forces with which we are acquainted are expressible
(though the exact relations of some have yet to be discovered) in terms of
work, it is found of great advantage to consider the power of doing work
as the common measure of doing all these. Thus, if we define energy as
that which does, or that which is capable of doing, work, we have a term
extremely convenient in the description of some aspects of our subject.
Thus we can now speak of the energies of nature, instead of the forces.
And all forces, active or passive, may be summed up in one word—energy.
And, further, the great discovery of the conservation of forces under definite
equivalents, may be summed up very briefly in this statement—THE AMOUNT
OF ENERGY IN THE UNIVERSE IS CONSTANT. To make this statement
clear requires that a distinction between two forms of every kind of energy
be pointed out. To recur to the example before imagined: if you carry the
1 lb. weight up the Monument, and deposit it on the ledge at the top, it
might lie there for a thousand years before it was made to give back the
work you had performed upon it. That work has been, in a manner, stored
up by the position you have given to your weight. Now, in taking up the
weight, you expended energy—you really performed work: that is an instance
of energy in operation, and may be termed “actual energy.” In
what form does the energy exist during the thousand years we may suppose
your weight to lie at the top of the Monument? It is ready to yield up
your work again at any moment it is permitted to descend, and it possesses
therefore during the whole period a potential energy equal in amount to
the actual energy you bestowed upon it. A similar distinction between
actual and potential energy exists with regard to every form of force. If
by any means you separate an atom of carbon from an atom of oxygen,
you exert actual energy. The process is analogous to carrying up the
weight. The atoms when separated possess potential energy,—they can
rush together again, like the weight to the earth, and in doing so will give
out the work which was expended on their separation. A parallel illustration
might be drawn from electrical force.
A typical example of the storing up of energy is furnished by a crossbow.
The moment a man begins to bend the bow he is doing work, because
he pulls the string in opposition to the bow’s resistance to a change
in its form; and it is plain that the amount of energy thus expended is
measurable. Suppose, now, the bow has been bent and the string caught
in the notch, from which it is released by drawing the trigger when the
discharge of the bow is desired. The bow may be retained for an indefinite
period in the bent condition, and in this state it possesses, in the form
of potential energy, all the work which has been expended in bending it,
and which it will, in fact, give out, in some way or other, whenever the
trigger is drawn. To fix our ideas, let us suppose that to draw the string
over the notch required a pull of 50 lbs. over a space of 6 in.; that is equivalent
to 50 × ½ = 25 units of work. Now let the bow be used to shoot an
arrow weighing ¼ lb. vertically upwards. The height in feet to which the
arrow will rise multiplied into its weight in pounds will be the work done
upon it by the bow. Now, we say that experiment proves that in the case
supposed the arrow would rise just 100 ft., so that the work done by the
807bow (¼ × 100 = 25) would be precisely that done upon it. For the sake of
simplicity, we keep this illustration free from the mention of interfering
causes, which have to be considered and allowed for when the matter is
put to the real test of quantitative experiment. The instance of the crossbow
brings into notice a highly instructive circumstance, which is this:
the bow, which it may have taken the strength of a Hercules to bend, will
shoot its bolt by the mere touch of a child on the trigger. In the same
way, when a man fires a gun, he merely permits the potential energy contained
in the charge to convert itself into actual, or kinetic, energy. The
real source of the energy, in the case of the child discharging the crossbow,
is the muscular power of the man who drew it; the real source of the
energy in exploding gunpowder is the separation of carbon atoms from
oxygen atoms, and that has been done by the sun’s rays, as truly as the
string was pulled away from the bow by muscular power. If we turn our
attention to nitro-glycerine or to nitro-cellulose, we can, by following the
chemical actions giving rise to these substances, in like manner trace their
energies to our great luminary. The unstable union by which oxygen and
nitrogen atoms are locked up in the solid and liquid forms of nitro-cellulose
and nitro-glycerine is also the work of the sun; for nitrogen acids, or
rather nitrates, are produced naturally under certain electrical and other
conditions of the atmosphere, which are due, directly or indirectly, to the
sun’s action; and they cannot be formed artificially, except by imitating
the natural conditions, as by passing electric sparks through air, &c.
It will now be understood, as regards the wonderful relations between
animal and vegetable life, which have already been alluded to more than
once, how the sun, by expending actual energy, separates atoms of carbon
from atoms of oxygen in the leaves of plants, and confers upon these a position
of advantage, i.e., potential energy; and how animals, absorbing the
separated carbon in the form of food, and inhaling the separated oxygen
in the air they breathe, cause the conversion of the potential into actual
energy, which appears in the heat, movements, and vital functions of the
animal body. In coal we have the energy which plants absorbed from the
sun ages ago, stored up in a potential form. The carbon atoms are ready
to rush into union with oxygen atoms, and convert their energy of position
into the energies developed by chemical action, viz., heat, light, &c.
Energy is thus constantly shifting its form from actual to potential, and vice
versâ, and exhibiting itself under the various transformations of force, as
when sun-force changes to chemical action, chemical action to heat, heat
to electricity, &c. Energy is, indeed, the real modern Proteus—constantly
assuming different shapes, difficult to grasp if not held in fetters; now
taking on the form of a lion, now of a flame of fire, a whirlwind, a rushing
stream. As sober, literal matter of fact we catch glimpses of energy under
these very forms.
The greatest discovery of the age has, as already indicated, immediate
and important practical bearings. The amount of thought which, even in
the present day, is devoted by unscientific mechanics to the old problem
of perpetual motion is far greater than is generally supposed. The principle
of the conservation of energy shows that this is an impossibility; that the
inventor who seeks to create force might just as well try to create matter;
that the production of a perpetually moving self-sustaining machine is as
far removed from human power as the bringing into existence of a new
planet. In force, as in matter, the law is inexorable—ex nihilo nihil fit.
Again, knowing the definite amount of energy obtainable from the combustion
808of a pound of coal, we can compare the amount we actually procure
from it in our steam engines with this theoretical quantity as the limit towards
which our improvements should bring us continually nearer, but
which we can never exceed, or, indeed, even reach. The schemers of
perpetual motion are not the only class of speculators who pursue objects
which are incompatible with our principle. There are many who seek to
accomplish desirable ends by inadequate means: who, for example, are
aiming perhaps to accomplish the reduction of ores by a quantity of fuel
less than that mechanically equivalent to the work, or who conceive that
by adding to coal some substance which itself is unchanged, an indefinitely
greater amount of heat may be liberated by the combustion.
Enough has been said to show that the energies of animal life can be
traced to the sun as their source. The sun builds up the plant, separating
oxygen from carbon. The animal—directly or mediately by devouring other
animals—takes the carbonaceous matter of the plant, and reunites it with
oxygen. In the plant the sun winds up the spring which gives life to the
animal mechanism; for the winding-up of a spring and the separation of
the atoms having chemical affinities are alike instances of supplying potential
energy. In the animal there is a running-down of the potential into
actual energy. It is plain also that of the total energy radiated from the sun
in every direction, the earth receives but a very small part (1 2300000000).
By far the larger part is diffused into space, where, for all such purposes
as those with which we are concerned, it is lost. The heat which the sun
sends out in a year is calculated to be equal to that which would be produced
by the combustion of a layer of coal 17 miles thick over the whole
surface of the luminary. Is the sun, then, a flaming fire? By no means.
Combustion is not possible at its temperature; and as we know the substances
which enter into its composition are the same as those we find in
the earth, we know that the chemical energies of such substances could not
supply the sun’s expenditure. Passing over as unsatisfactory an explanation
which might occur to some minds—namely, that the sun was created
hot at the beginning, and has so continued—there are two theories which
attempt to account for the sun’s heat. One is that of Meyer, who supposes
the heat is due to the continual impact of meteorites drawn to the sun by
its gravity; and the other is that of Helmholtz, who attributes the heat to
the continual condensation of the substance of the sun. Helmholtz calculates
that a shrinking of the sun’s diameter by only 1 10000th of its present
amount, would supply heat to last for two thousand years; while the condensation
of the substance of the sun to the density of the earth would
cover the sun’s expenditure for 17,000,000 of years. There is great probability
that both theories may be correct, and that the cause of the sun’s
heat may be considered as due in general terms to aggregation of matter,
by which the original potential energy of position is converted into the
actual energy of heat and light. Now, however immense may be our planetary
system, the sun being continually throwing off this energy into space,
there must come a time when the supplies of meteorites will fail, and when
the great globe of the sun will have shrunk to its smallest dimensions. We
see, then, that heat and light are produced by the aggregation of matter;
the heat and light are radiated into space; the small fraction intercepted
by our globe is the source of almost every movement—the original stuff, so
to speak, out of which all terrestrial forces are made. The sun produces
the winds, the thunderstorms, the electric currents of the Aurora, the phenomena
of terrestrial magnetism, and is the source of vegetable and animal
809life. The waves, the rains, the mountain torrents, the flowing rivers, are
the work of the sun’s emanations.
In the illustration of the energy expended on raising a weight afterwards
dropped, we traced that energy into the final form of heat of a low temperature
radiated into space. It would be easy to show that all energy ultimately
takes the same form. Now, although it is easy to convert work into heat,
there is no conceivable process by which uniformly-diffused heat can again
be made to do any kind of work. The case may be compared to water,
which in moving down from a higher to a lower level may be made to perform
any variety of work. But when all the water has passed down from the
higher level to the lower, it can no longer do any work. Whenever work is
done by the agency of heat, there is always a passing from a higher temperature
to a lower—a transference of heat from a hotter body to a colder. If
the condenser of the steam engine had the same temperature as the steam,
the machine would not work. Not only do all the energies in operation on
the face of the earth continually run down into the form of radiant heat
sent off by the earth into space; but our sun’s energy, and that of the suns
of other systems, are also continually passing off into space; and the final
effect must be a uniform diffusion of heat in a universe in which none of
the varied forms of energy we now behold in operation will be possible,
because all will have run down to the same dead level of uniformly-diffused
heat. This startling corollary from the principle of the conservation of
energy has been worked out by Sir W. Thomson under the title of “The
Dissipation of Energy.” It leads us to contemplate a state of things in
which all light and life will have passed away from the universe—a condition
which the poet’s terrible dream of darkness, “which was not all a
dream,” seems to shadow forth—
The waves were dead; the tides were in their grave,
The Moon, their mistress, had expired before;
The winds were withered in the stagnant air,
And the clouds perished; Darkness had no need
Of aid from them—She was the Universe.”
The doctrine of this persistence and dissipation of energy completely
harmonizes with the grand speculation termed the “nebular hypothesis,”
which regards the universe as having originally consisted of uniformly diffused
matter, which, being endowed with the power of gravitation, aggregated
round certain centres. This process is still going on; and, according to
modern speculations, light and life and motion are but manifestations of
this primæval potential energy being converted into actual energy, and
degrading ultimately into the form of universally-diffused heat. To quote
the closing sentences of the eloquent passage in which Professor Tyndall
concludes the work mentioned above, “To nature nothing can be added,
from nature nothing can be taken away; the sum of her energies is constant,
and the utmost man can do in the pursuit of physical truth, or in the
810applications of physical knowledge, is to shift the constituents of the never-varying
total. The law of conservation rigidly excludes both creation and
annihilation. Waves may change to ripples, and ripples to waves; magnitude
may be substituted for number, and number for magnitude; asteroids
may aggregate to suns, suns may resolve themselves into floræ and
faunæ, and floræ and faunæ melt in air: the flux of power is eternally the
same. It rolls in music through the ages, and all terrestrial energy—the
manifestations of life as well as the display of phenomena—are but the
modulations of its rhythm.”
The discoveries to which we have here endeavoured to attract the reader’s
attention thus give rise to conceptions of the utmost grandeur and interest.
We see that the sum of Nature’s energies is constant; that all the manifestations
of force are but the transference of power from one position to
another. And we have recognized the material source of all our terrestrial
energies in the sun. Two theories have already been mentioned by which
it is sought to account for the sun’s heat—the meteoric theory of Meyer and
Thomson, and the shrinkage theory of Helmholtz. These both assume
gravitation as the primal force from which the supply of heat and other
energies must be drawn, and they assume also that the laws of radiation
and of the degradation of temperature in the transformation of heat into
other forces, as we find them operating at the earth’s surface, are equally
in action in every region of space. Hence is deduced that conception of
the final state of the universe as one of merely equally diffused temperature
admitting of no further transformation. This speculation presents
the universe in the aspect of a clock, now indeed going, but when once
run down, incapable of ever being again wound up. There seems in this
view a want of symmetry, so to speak; we miss the feeling of harmonious
rhythm to which Tyndall refers. There is, however, another cosmic
theory, well supported by accumulating facts, which assigns to gravitation
a less important part in the production of solar heat and in the evolution
of worlds, and it is one which supplies also a basis for the explanation of
such phenomena as aerolites, comets, variable stars, the inclination of
planets’ axes to their orbits, the proper motion of our sun, and that of the
so called fixed stars, of all of which the nebular hypothesis fails to give
any account; while, on the other hand, the impact theory, as it has been
named, includes the other, and goes beyond it. The reader who desires
to pursue this subject may be referred to Croll’s book on Stellar Evolution.
In the last few paragraphs we have been dealing with speculations as
much as with discoveries. But indeed the former are the offspring of the
latter, as certainly as one invention becomes the parent of others. The
human mind never rests contented with the knowledge and mastery of
nature actually gained, but ever seeks to pass beyond and attain still
greater power. The volume we are now bringing to a close has given
but brief and imperfect indications of specimens, taken here and there, of
what has been done during the short period of one century. We may
draw an augury for the future of man’s dominion from the powers his
Promethean spirit has already grasped:
“The lightning is his slave; heaven’s utmost deep
Gives up her stars, and like a flock of sheep
They pass before his eye, are numbered, and roll on!
The tempest is his steed, he strides the air;
And the abyss shouts from her depth laid bare,
“Heaven, hast thou secrets? Man unveils me; I have none.”
NOTES A and B. — Note A — Continuation of Table on page 755 , showing the quantity of Coals raised annually in Great Britain. — Note B — CONSERVATION OF ENERGY. — Page 804 .
811
812
Year.
Coal raised in Tons.
1874
126,590,108
1875
133,306,458
1876
134,125,166
1877
134,179,968
1878
132,612,063
1879
133,720,393
1880
146,969,409
1881
154,184,300
1882
156,499,977
1883
163,737,327
1884
160,757,779
1885
159,351,418
1886
157,518,482
1887
162,121,576
1888
169,935,219
1889
176,916,724
1890
181,614,280
1891
185,479,126
1892
181,786,871
1893
164,325,795
1894
188,277,525
The statement here should have been more explicit, as it has reference
to a state of things not to be realised in practice. Like the well-known
“first law of motion,” it can neither be demonstrated à priori, nor proved
by any direct and simple experiment. The first law of motion asserts
that a body in motion, not acted on by any external force, will continue
to move in a straight line, and with a uniform velocity. Now we cannot
place a body in such a position that it will not be acted upon by some external
forces; but the more we lessen the effect of external forces, the
more nearly is the motion straight and uniform. Similarly in the case
supposed, the intention is to show that the weight carried up is in a
position to do just as much work as was done upon it. We must suppose
several impracticable but conceivable conditions in order to eliminate considerations
which do not concern the theoretical question; we must suppose
the cord to be weightless and absolutely devoid of rigidity; the
pulley to have no mass or inertia, that is to require no force to set it in
motion, and to move without any friction; the air to offer no resistance;
and the force of gravity to be uniform throughout the space. Some approximation
to these conditions is practicable, as, for example, the pulley
might be the lightest possible, and turn on friction wheels, the cord might
be the finest silk thread, and so on. But it is not the influence of these
external forces we are considering, but only the energy due to the position
of the raised weight. Assuming, therefore, the disturbing conditions
absolutely eliminated, it is not difficult to see that no downward force or
pressure, however small, could be applied for ever so short a time, to the
upper weight without setting the system in motion. The motion would
be an accelerated one so long as the force was applied, it would become
uniform when the force ceased to act; it would have a velocity proportionate
to the force. In any case, after a time the descending weight
would reach the ground, and for our point of view it is quite immaterial
whether the time occupied by the movement were 5 minutes or 5,000
years, for be it observed, time does not enter into the definition of work
as it does into that of “horse-power.” Then by pushing the conceived
conditions to their limits, we may see that without considering any
question of conversion of motion into heat, the raised weight can, in theory
at least, give back again the energy spent upon it.
Added “near Bristol” after “146. Clifton Suspension Bridge,” on p. xii.
Added “PLATE IX.” to caption of illustration facing p. 144.
Added “PLATE XI.” to caption of illustration facing p. 168.
Switched the captions for “Fig. 99.” facing p. 210 with the caption
for “Fig. 102” facing p. 206. The captions were out of order and did not
agree with the content of the illustration.
Changed “a calibre of 4,724 in.” to “a calibre of 4·724 in.” on p. #208.
Otherwise the muzzle opening would be larger than its length. Confirmed online.
Changed “the two rows in” to “the two rows is” on p. 332.
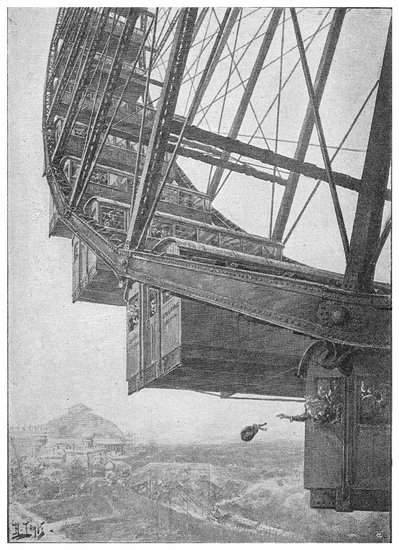

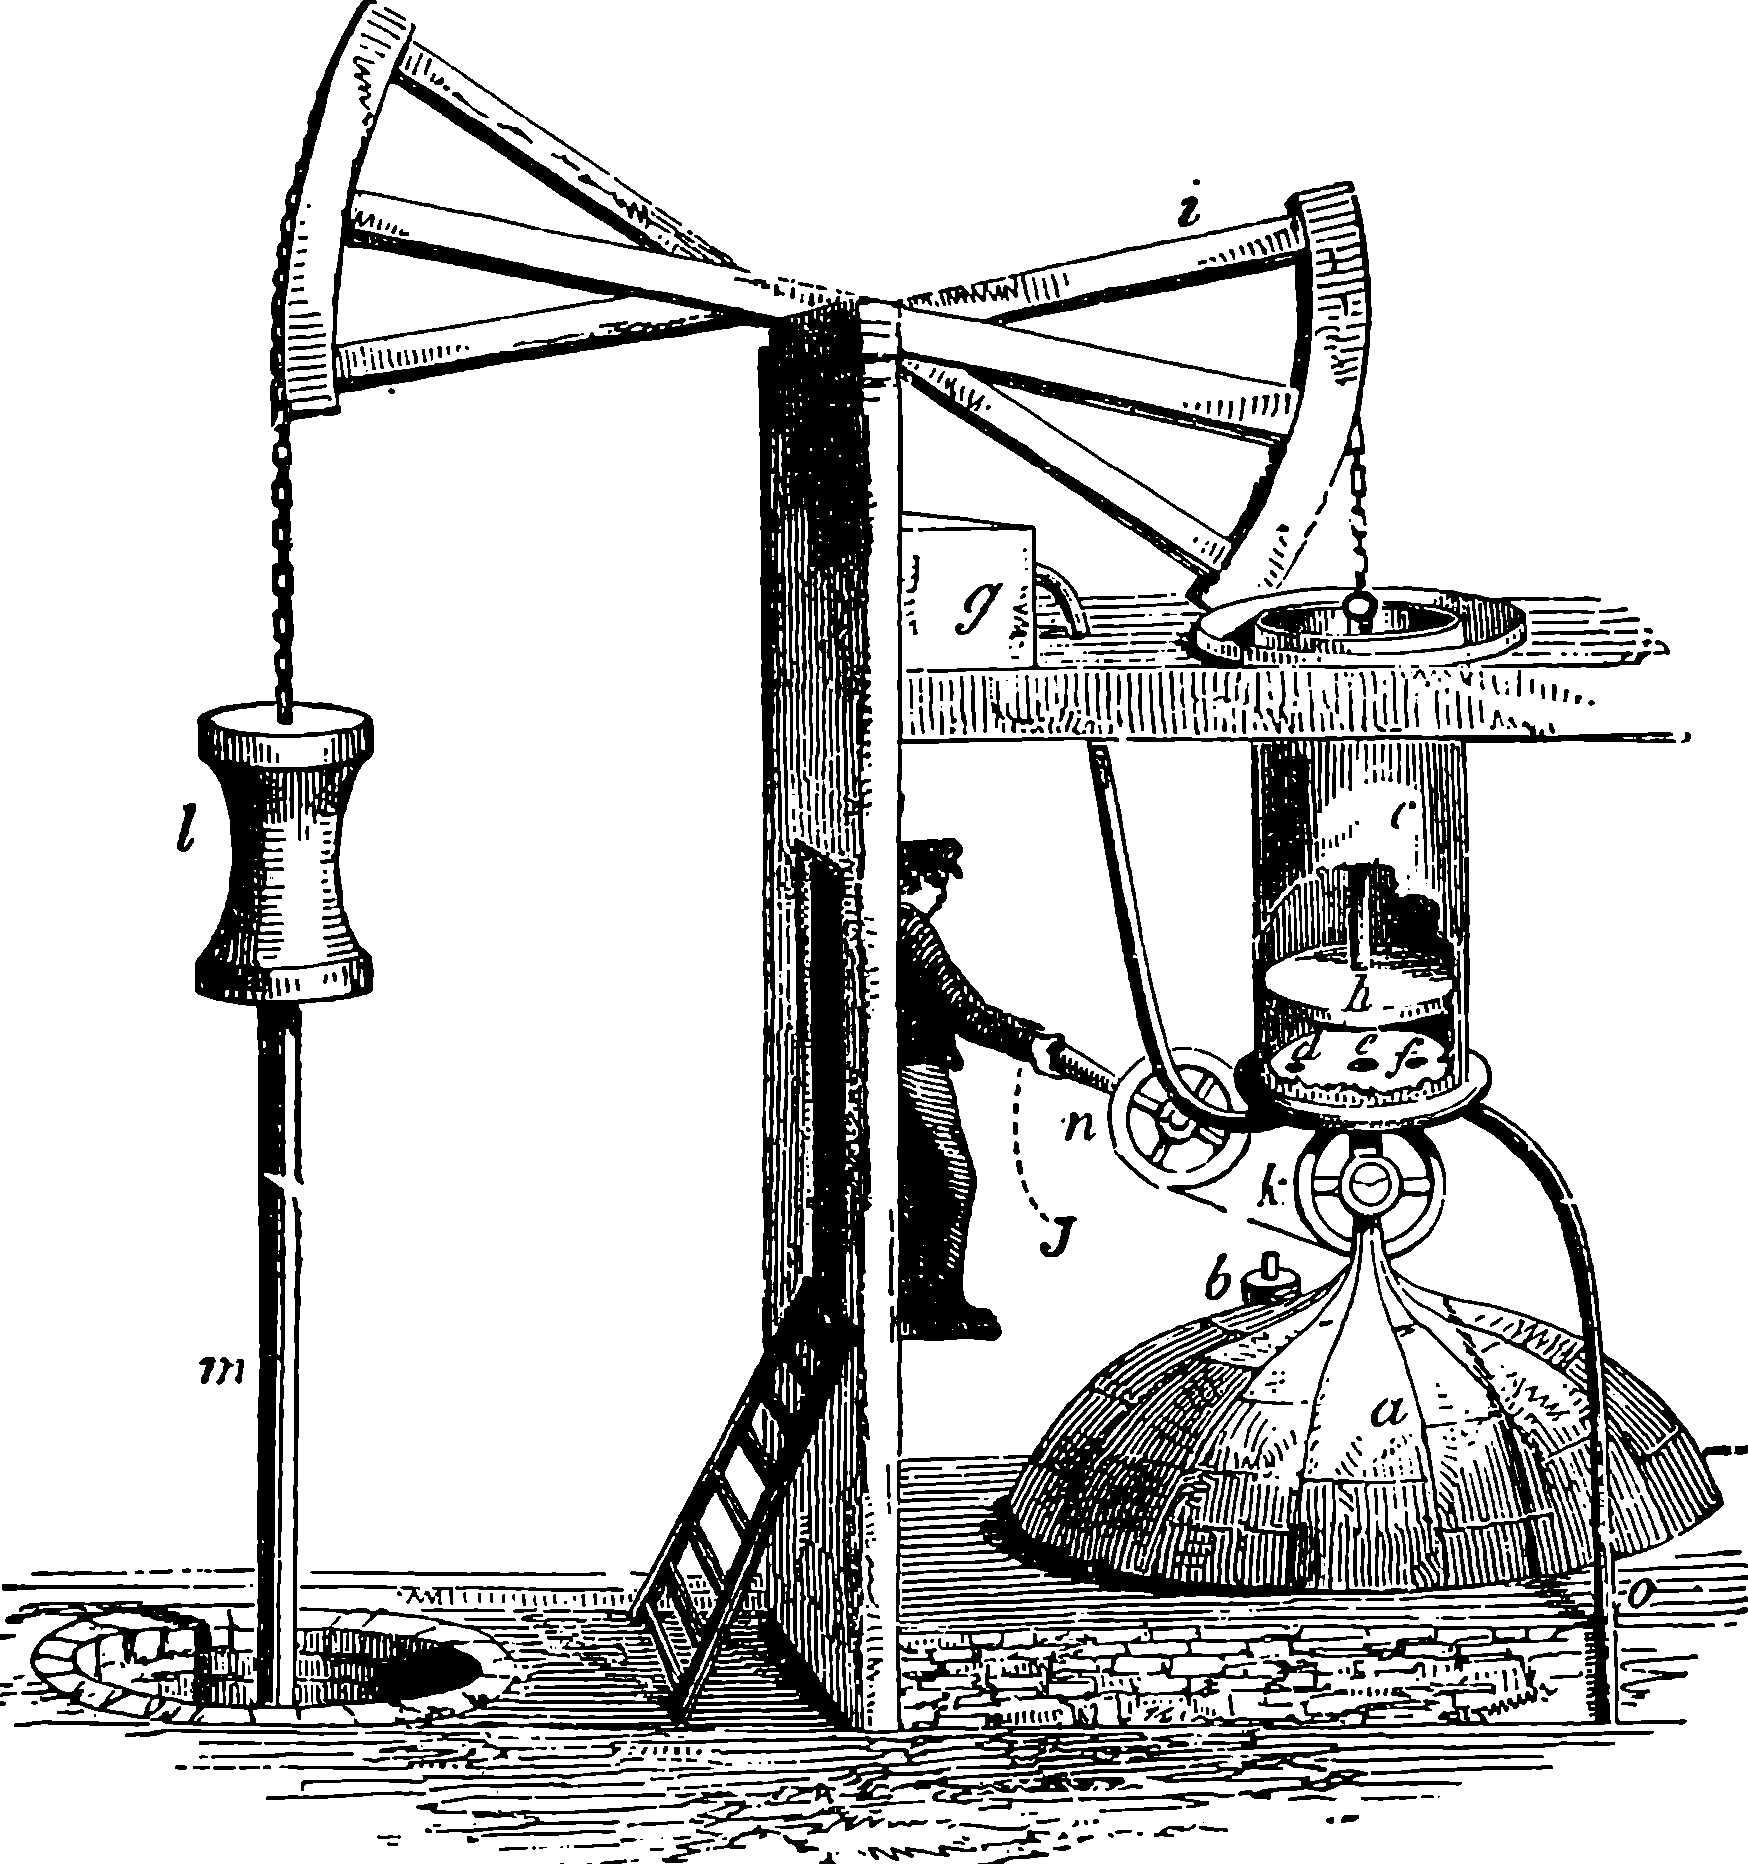
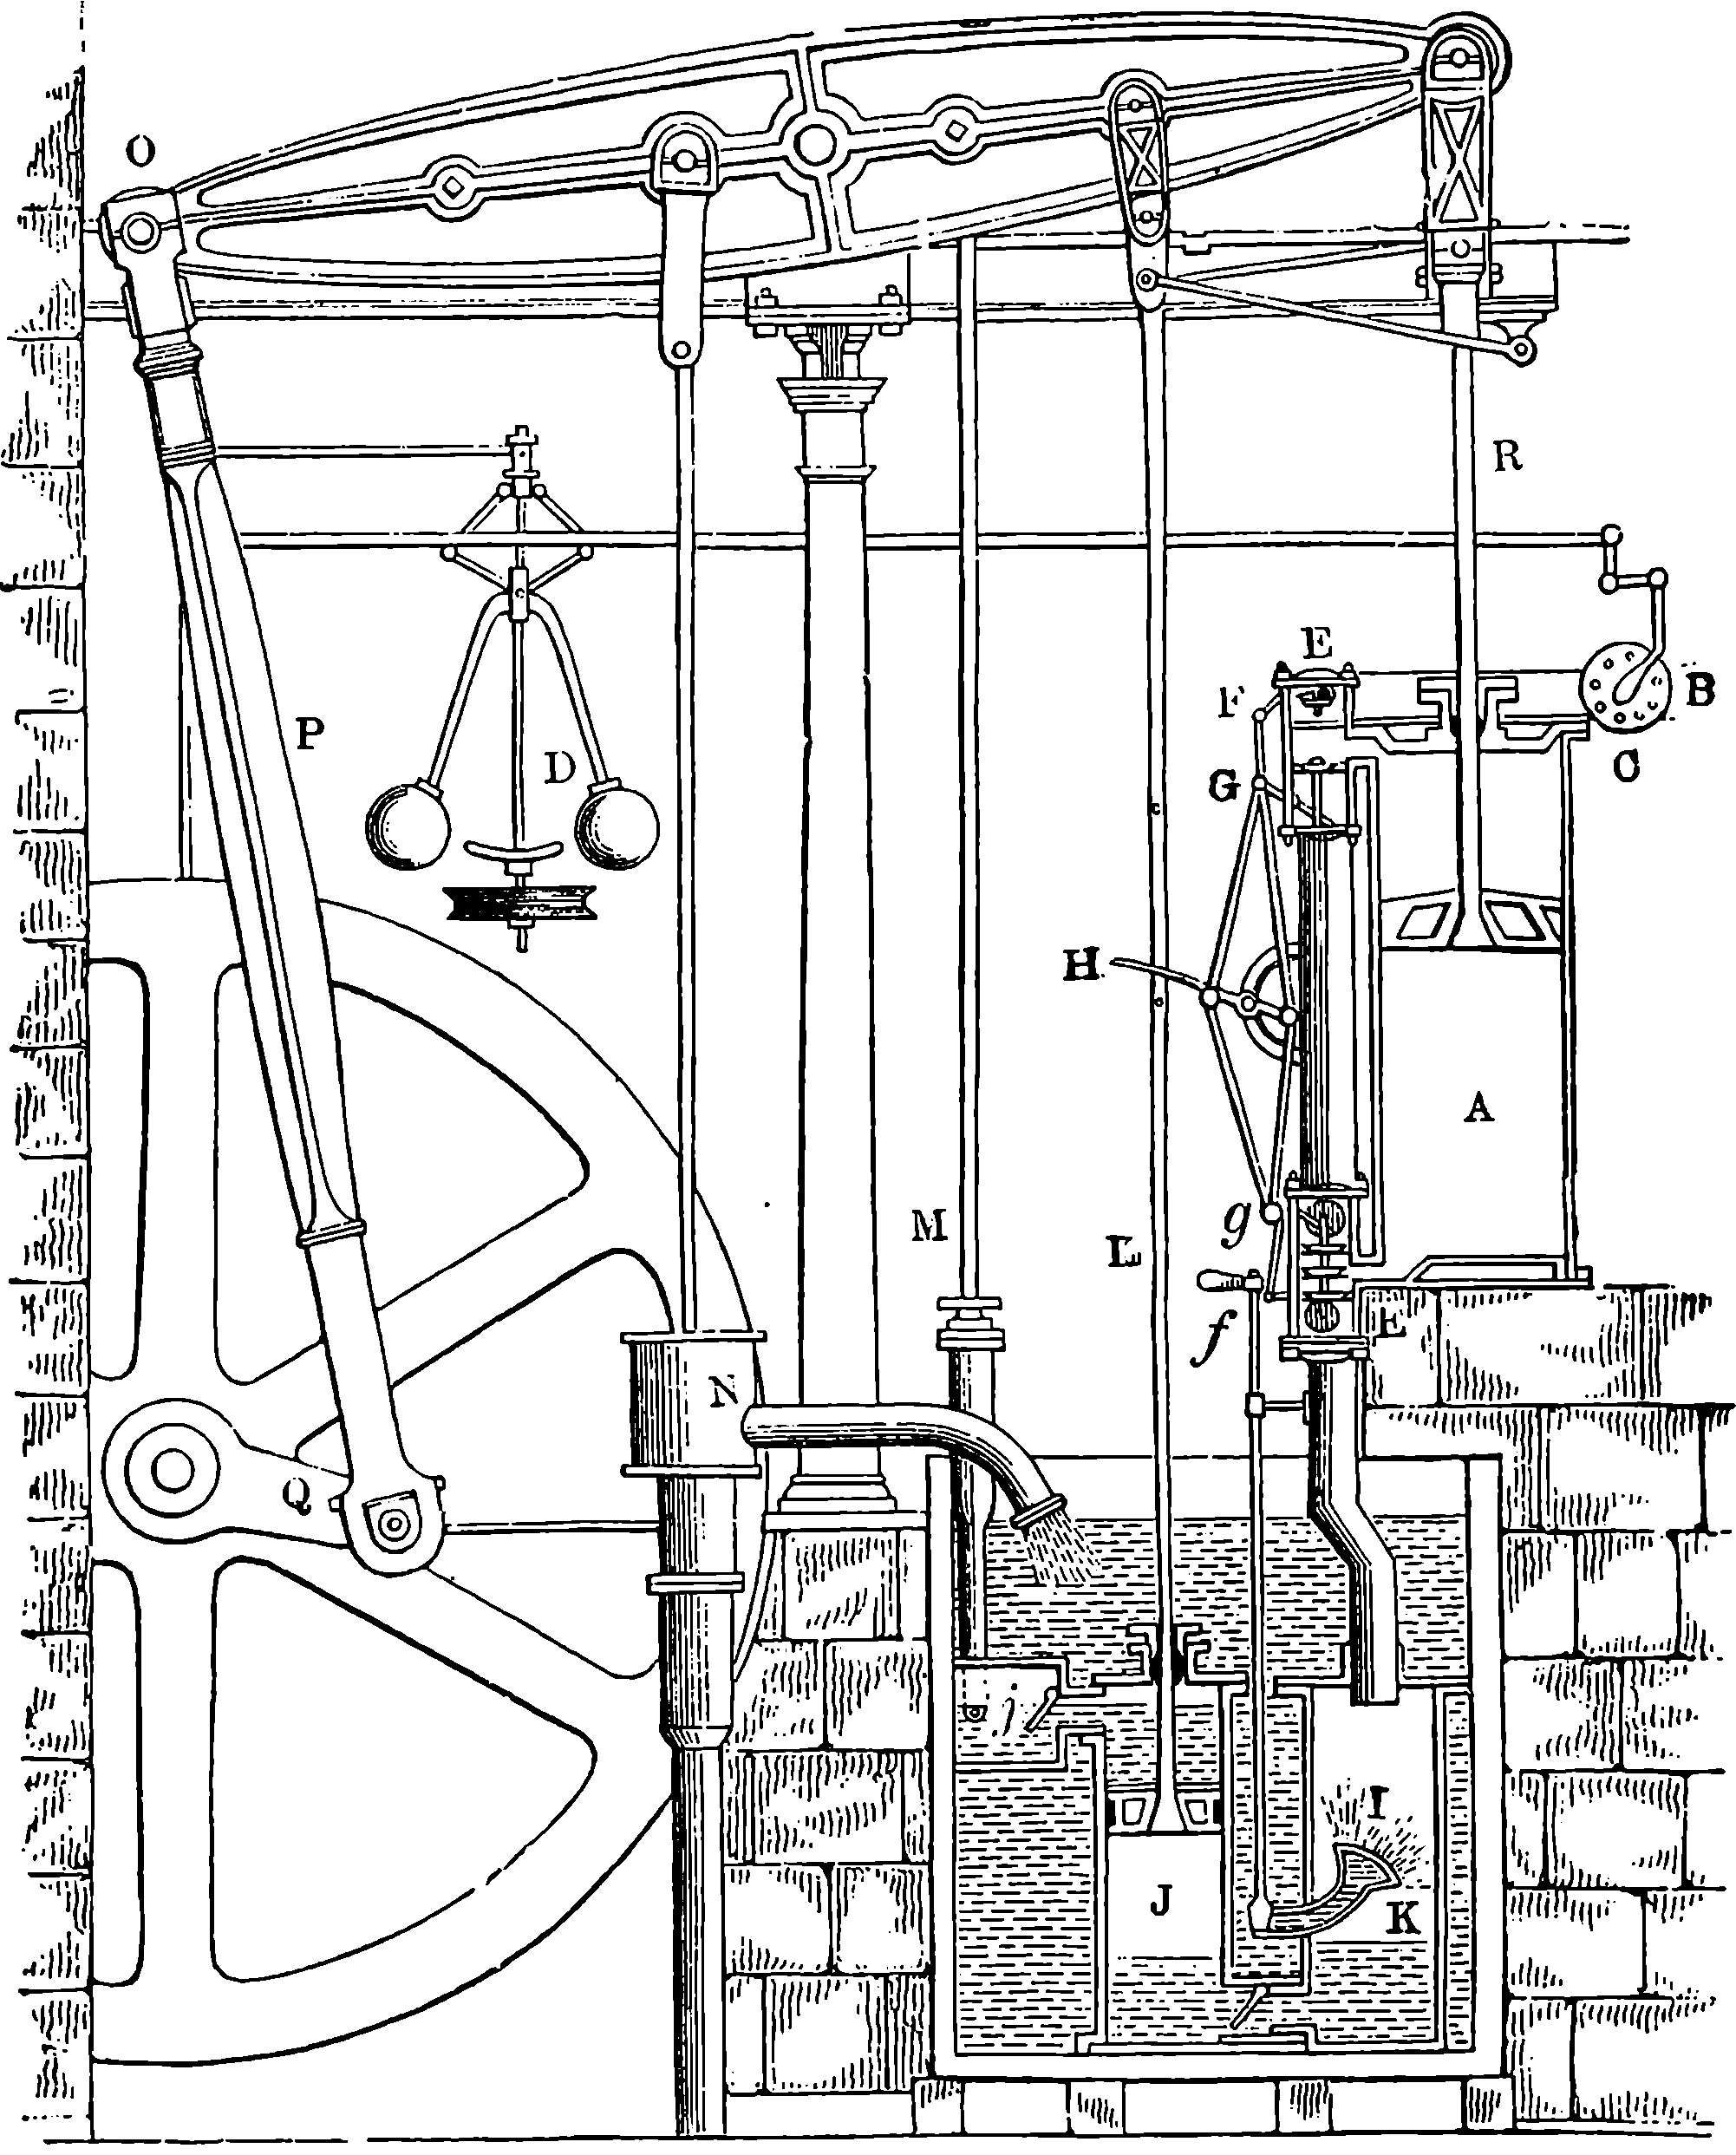
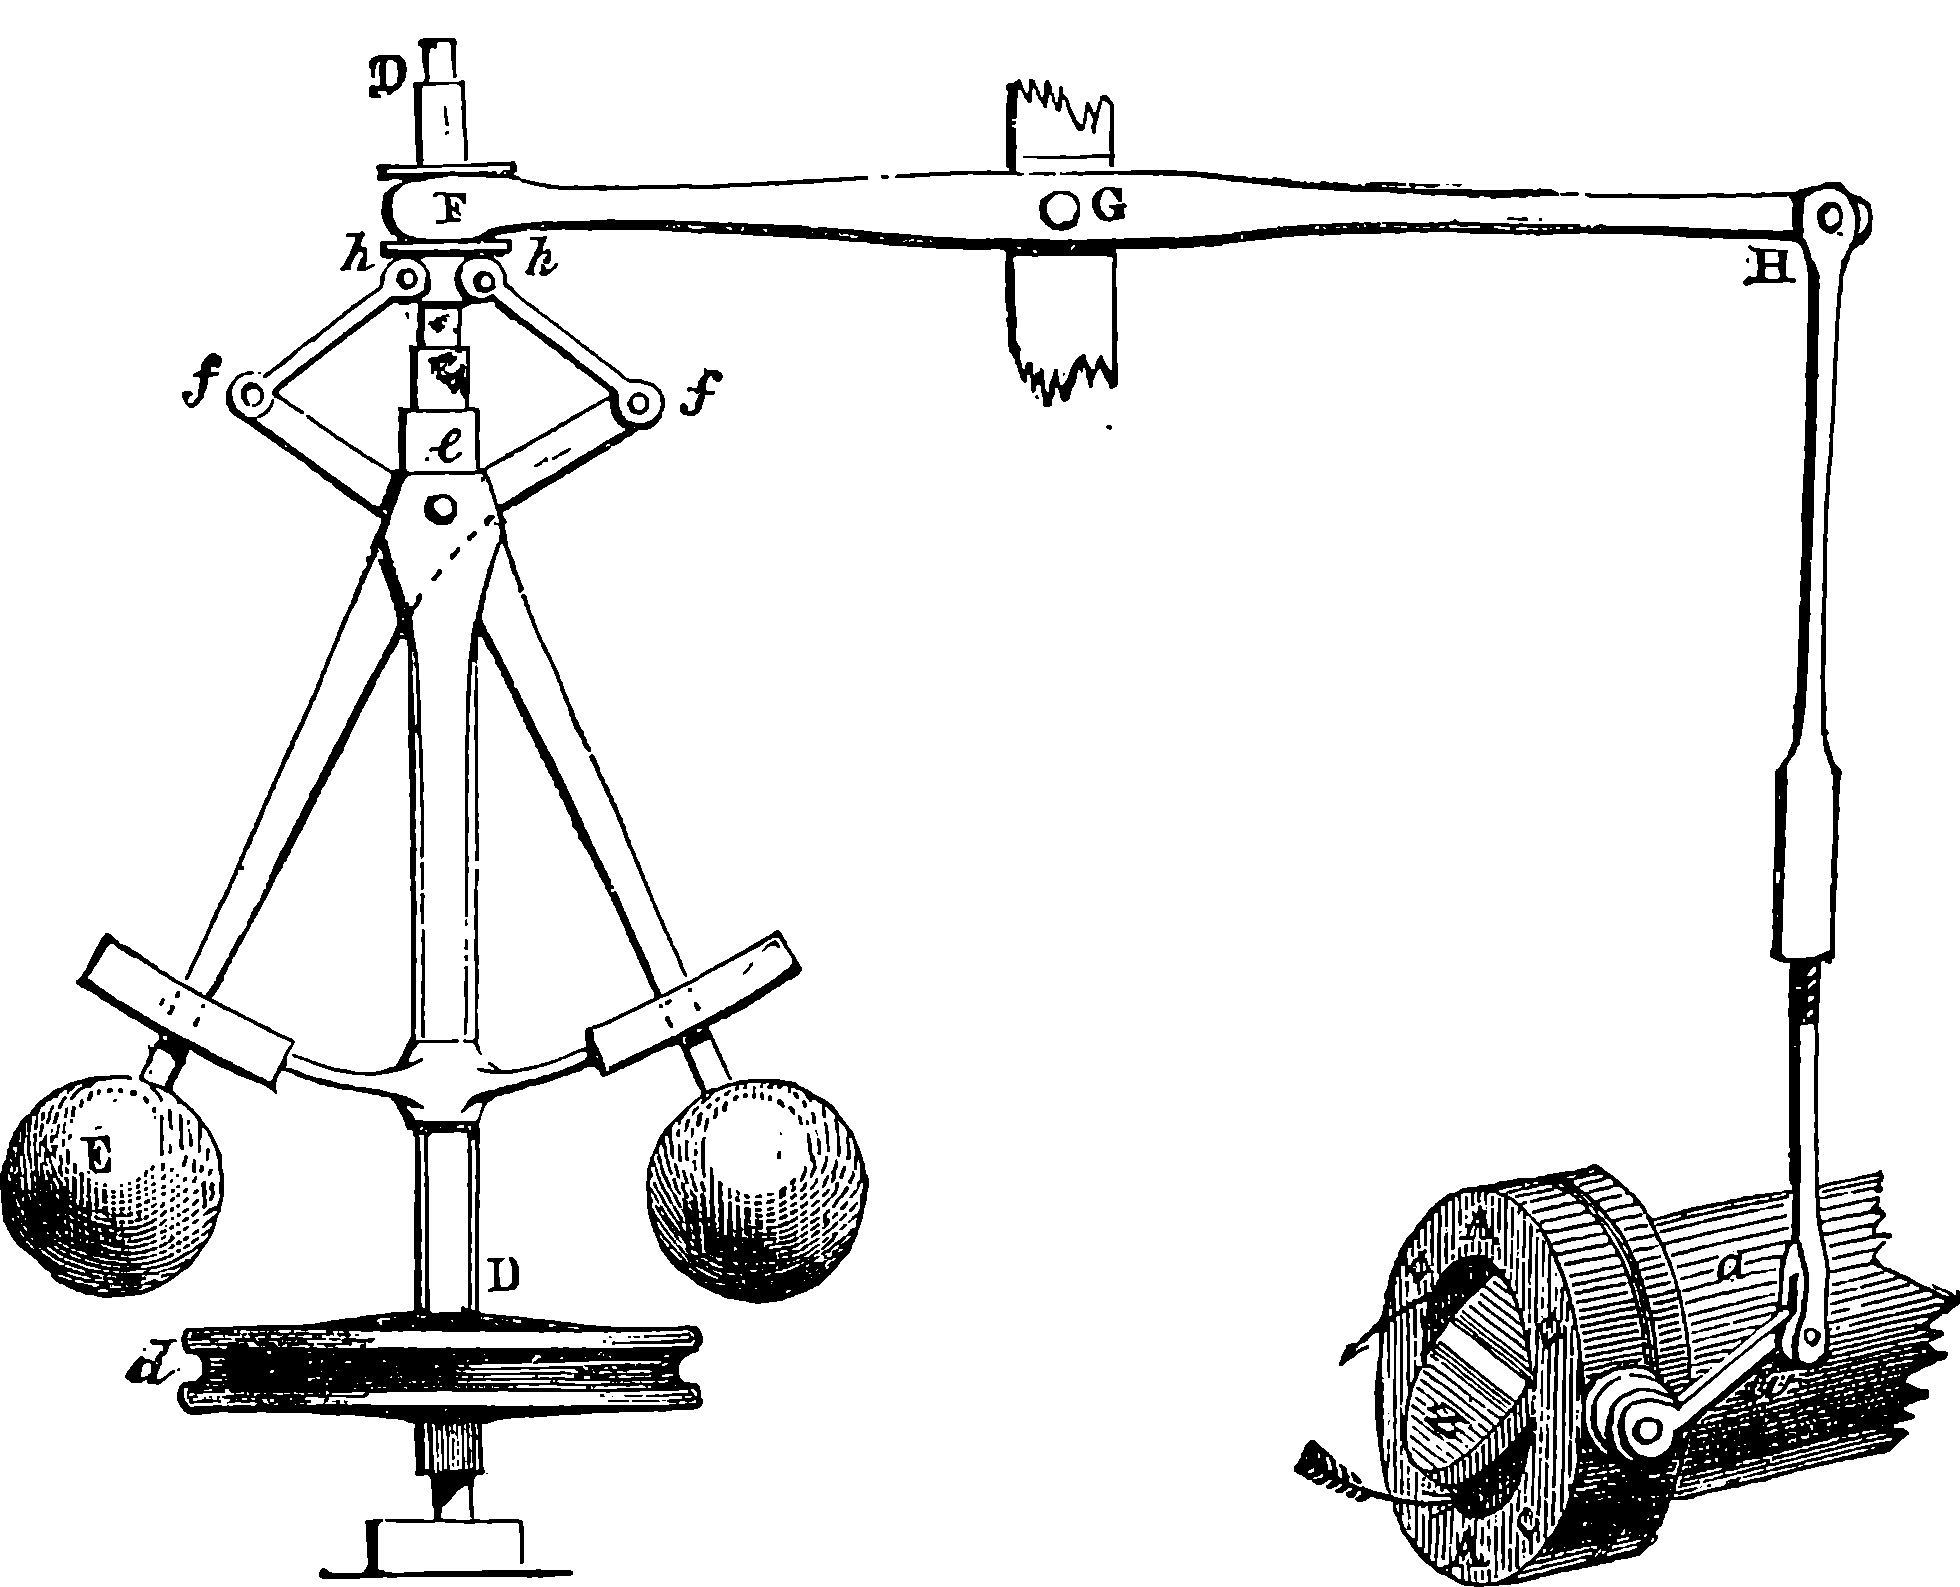
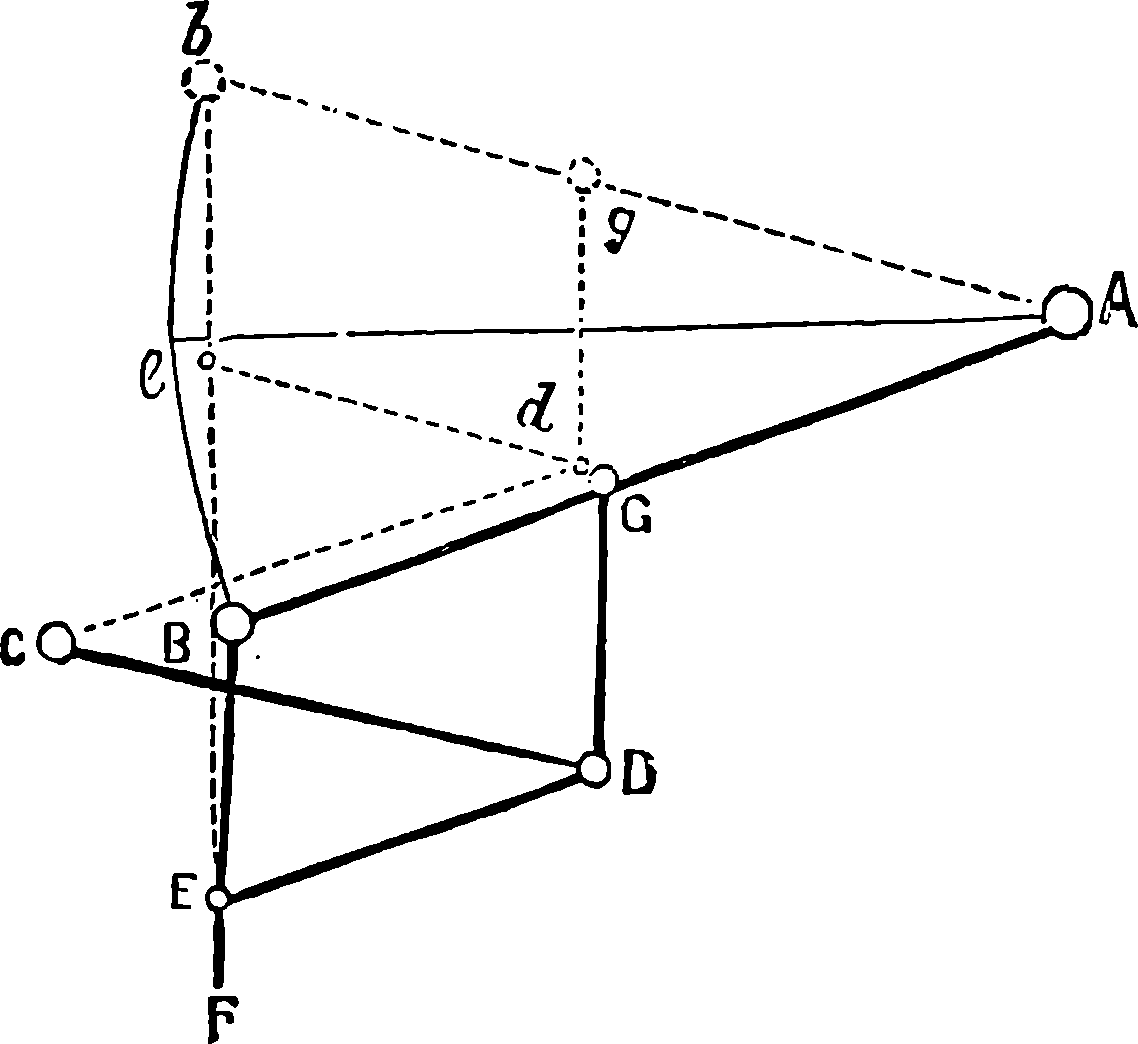
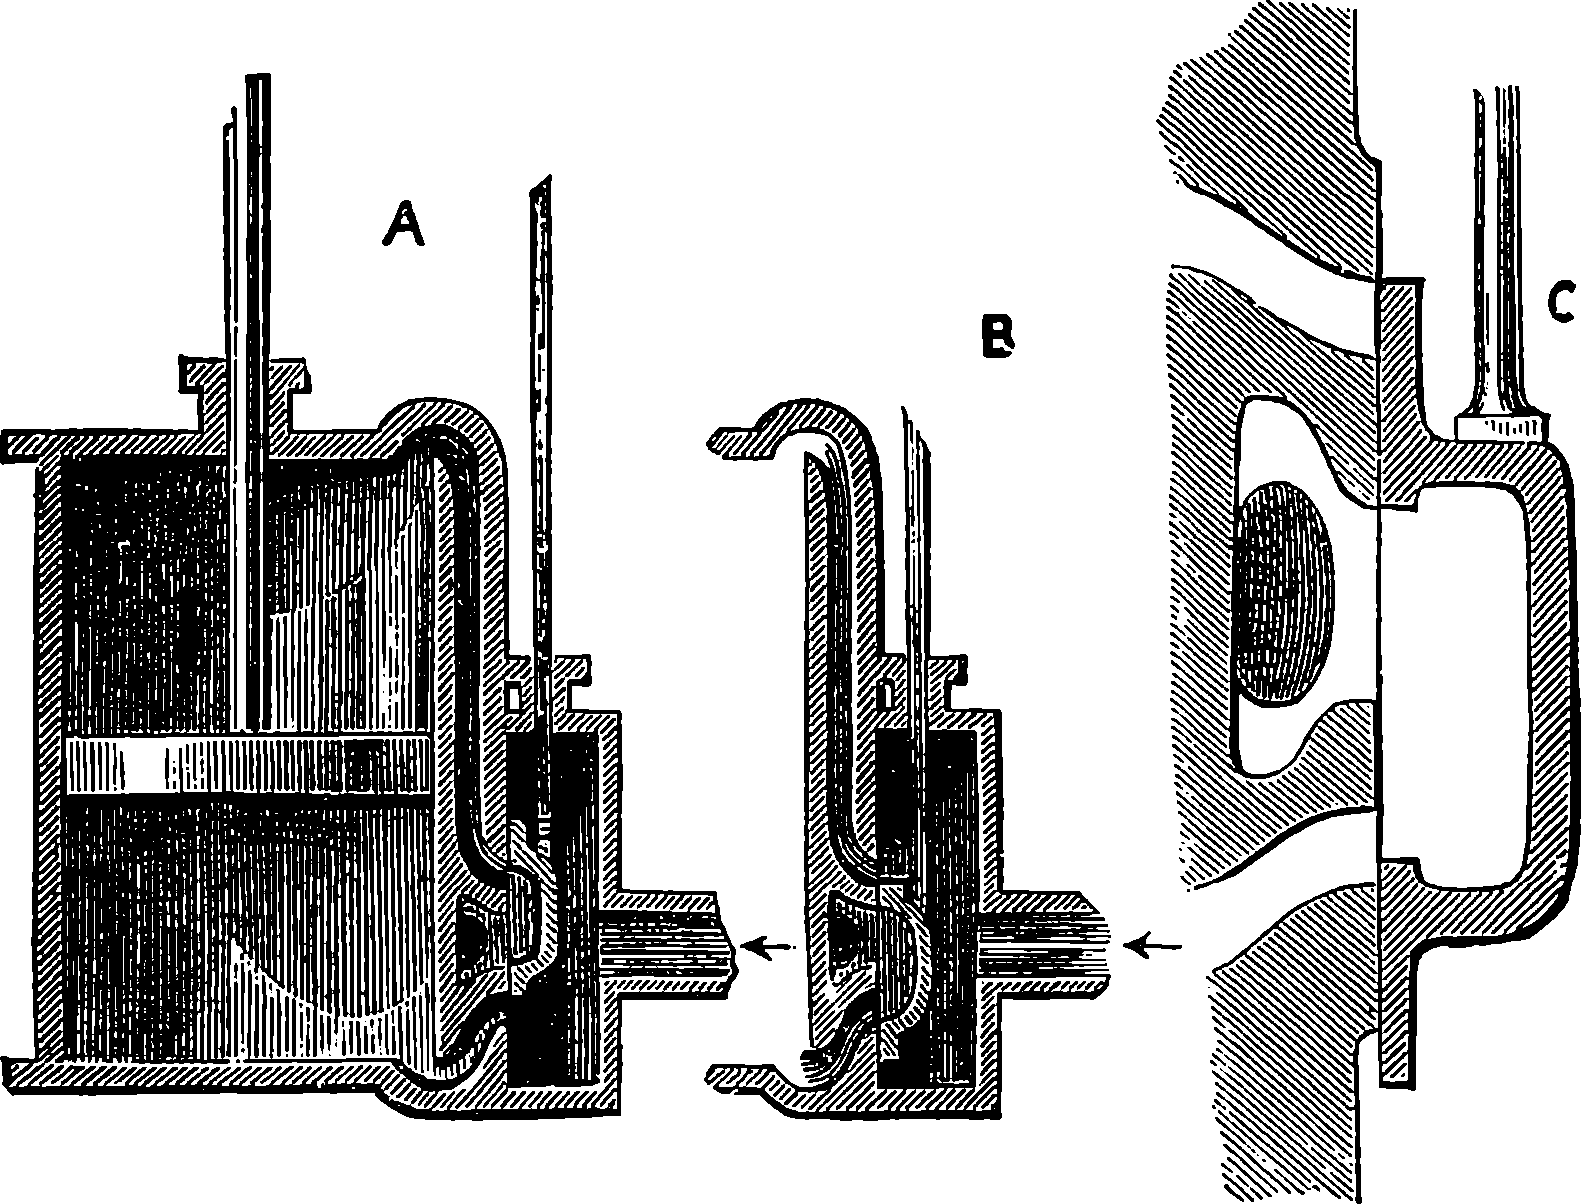
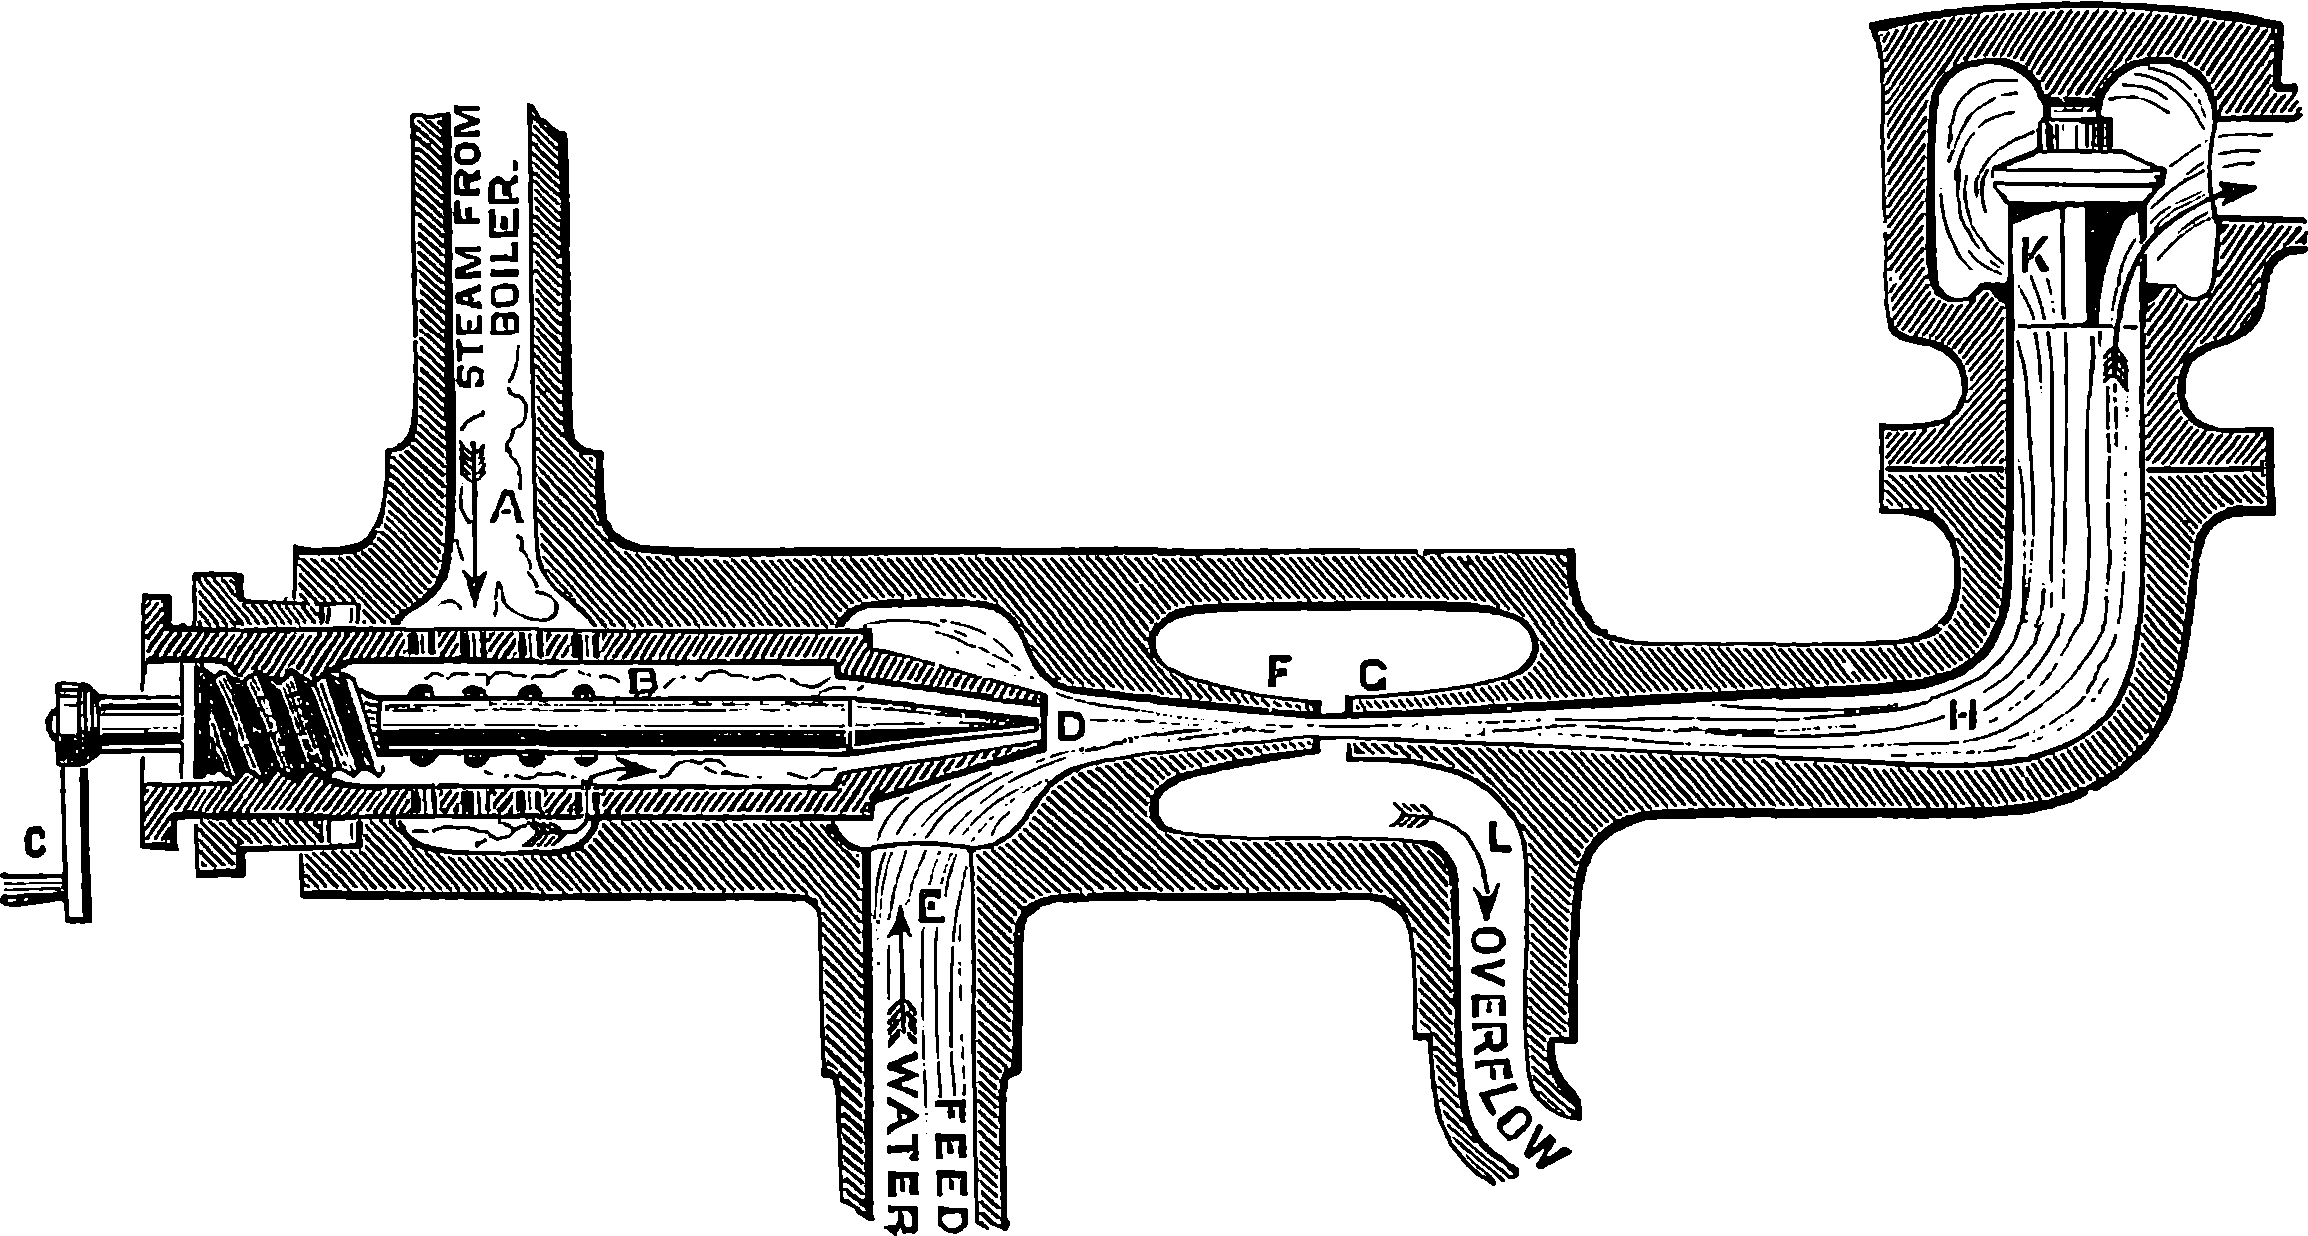
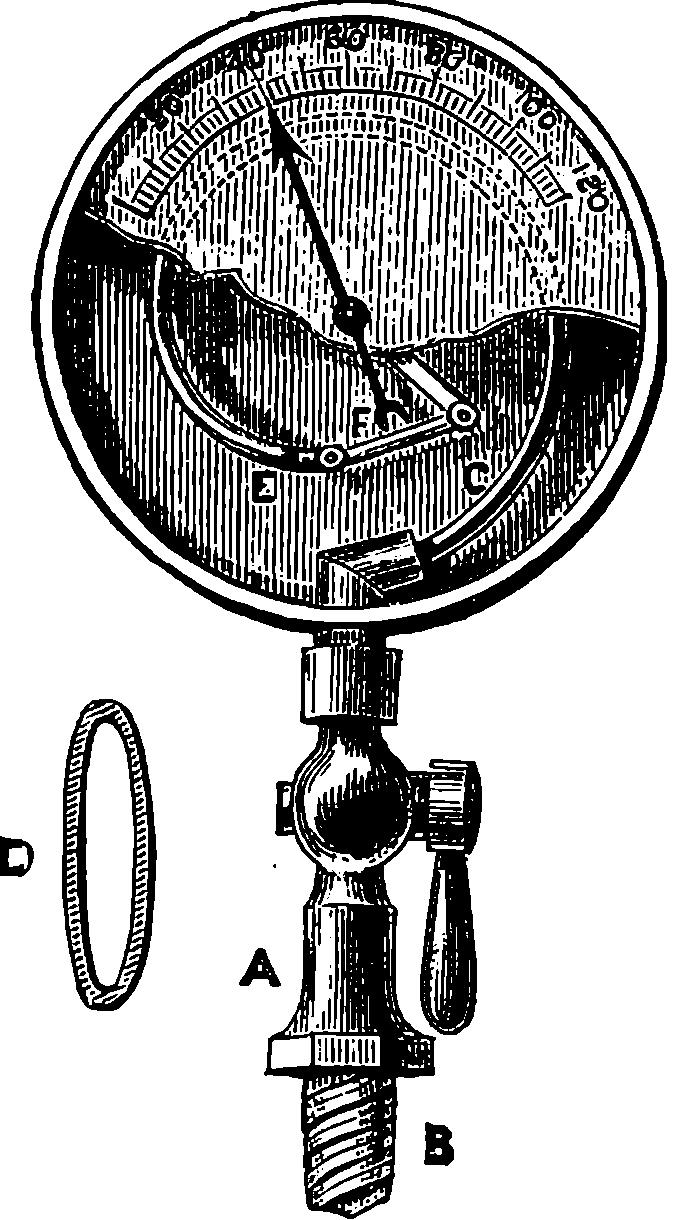
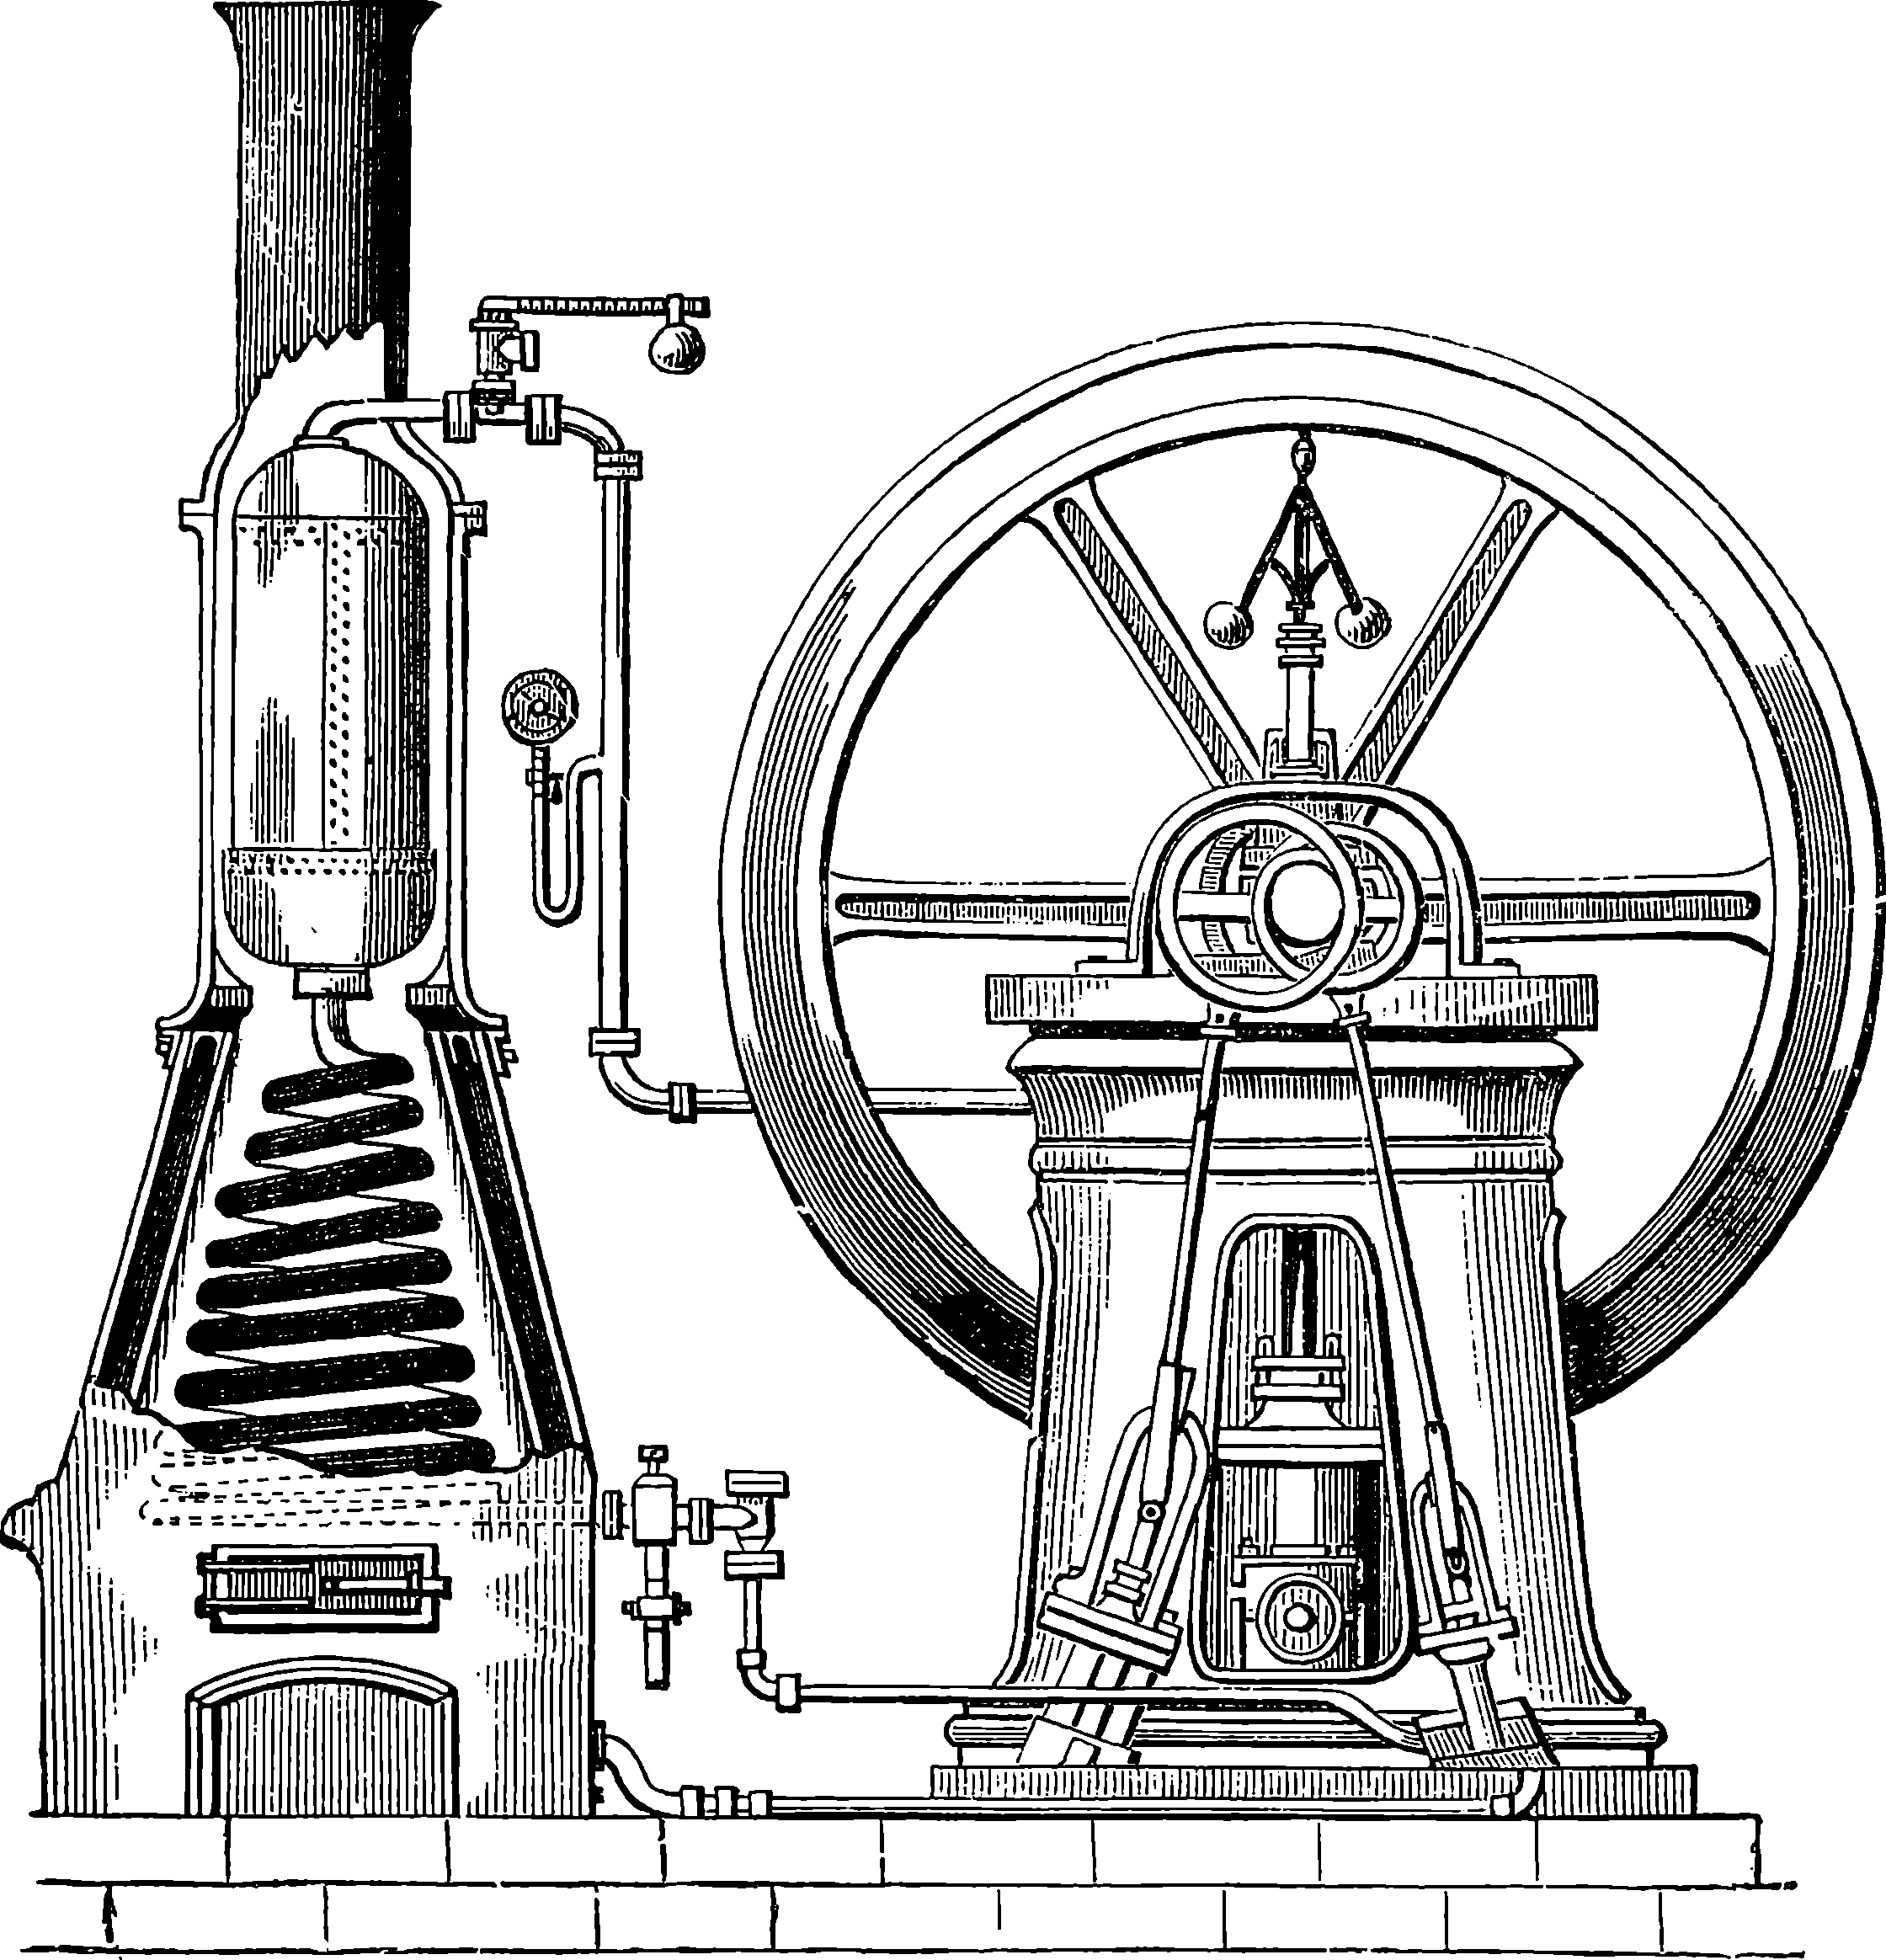
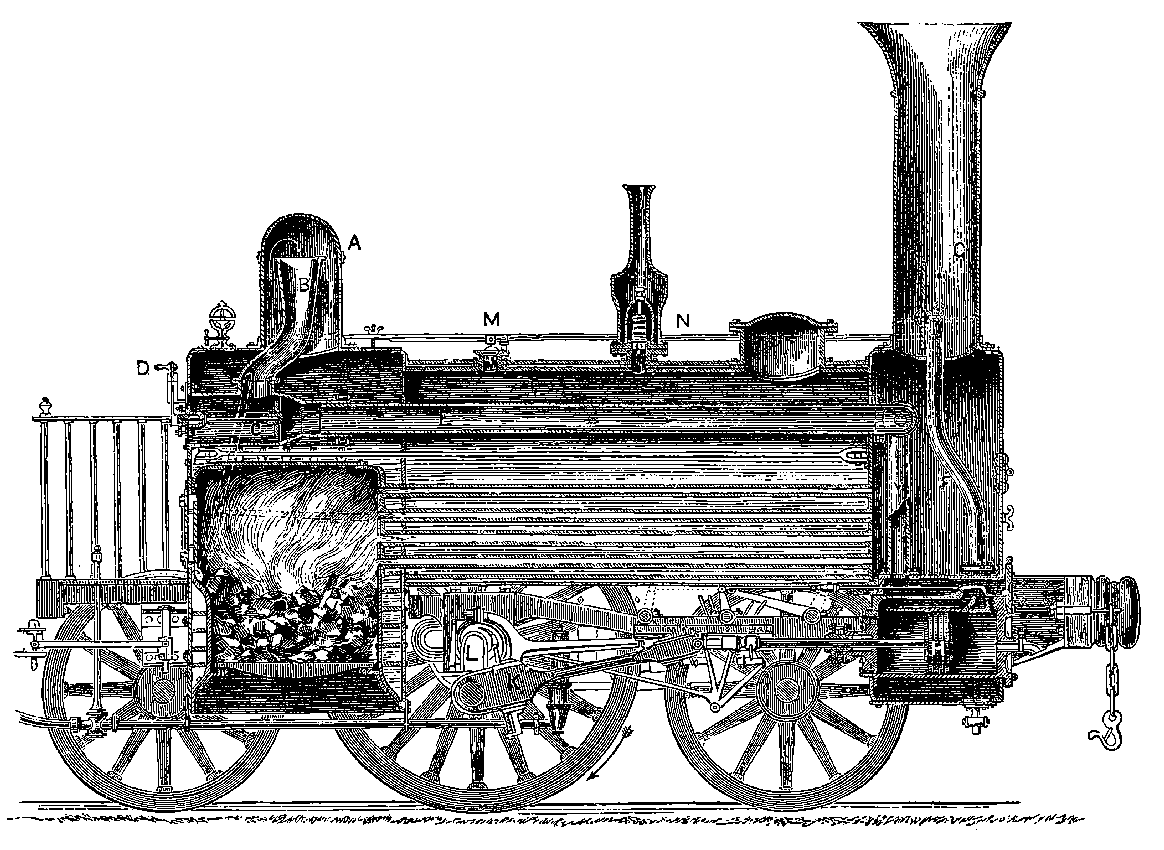
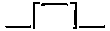 ; and the crank bendings for the two cylinders are
placed in planes at right angles to each other, so that when one is at the
“dead point,” the other is in a position to receive the full power of the
piston. There are two safety valves, one at
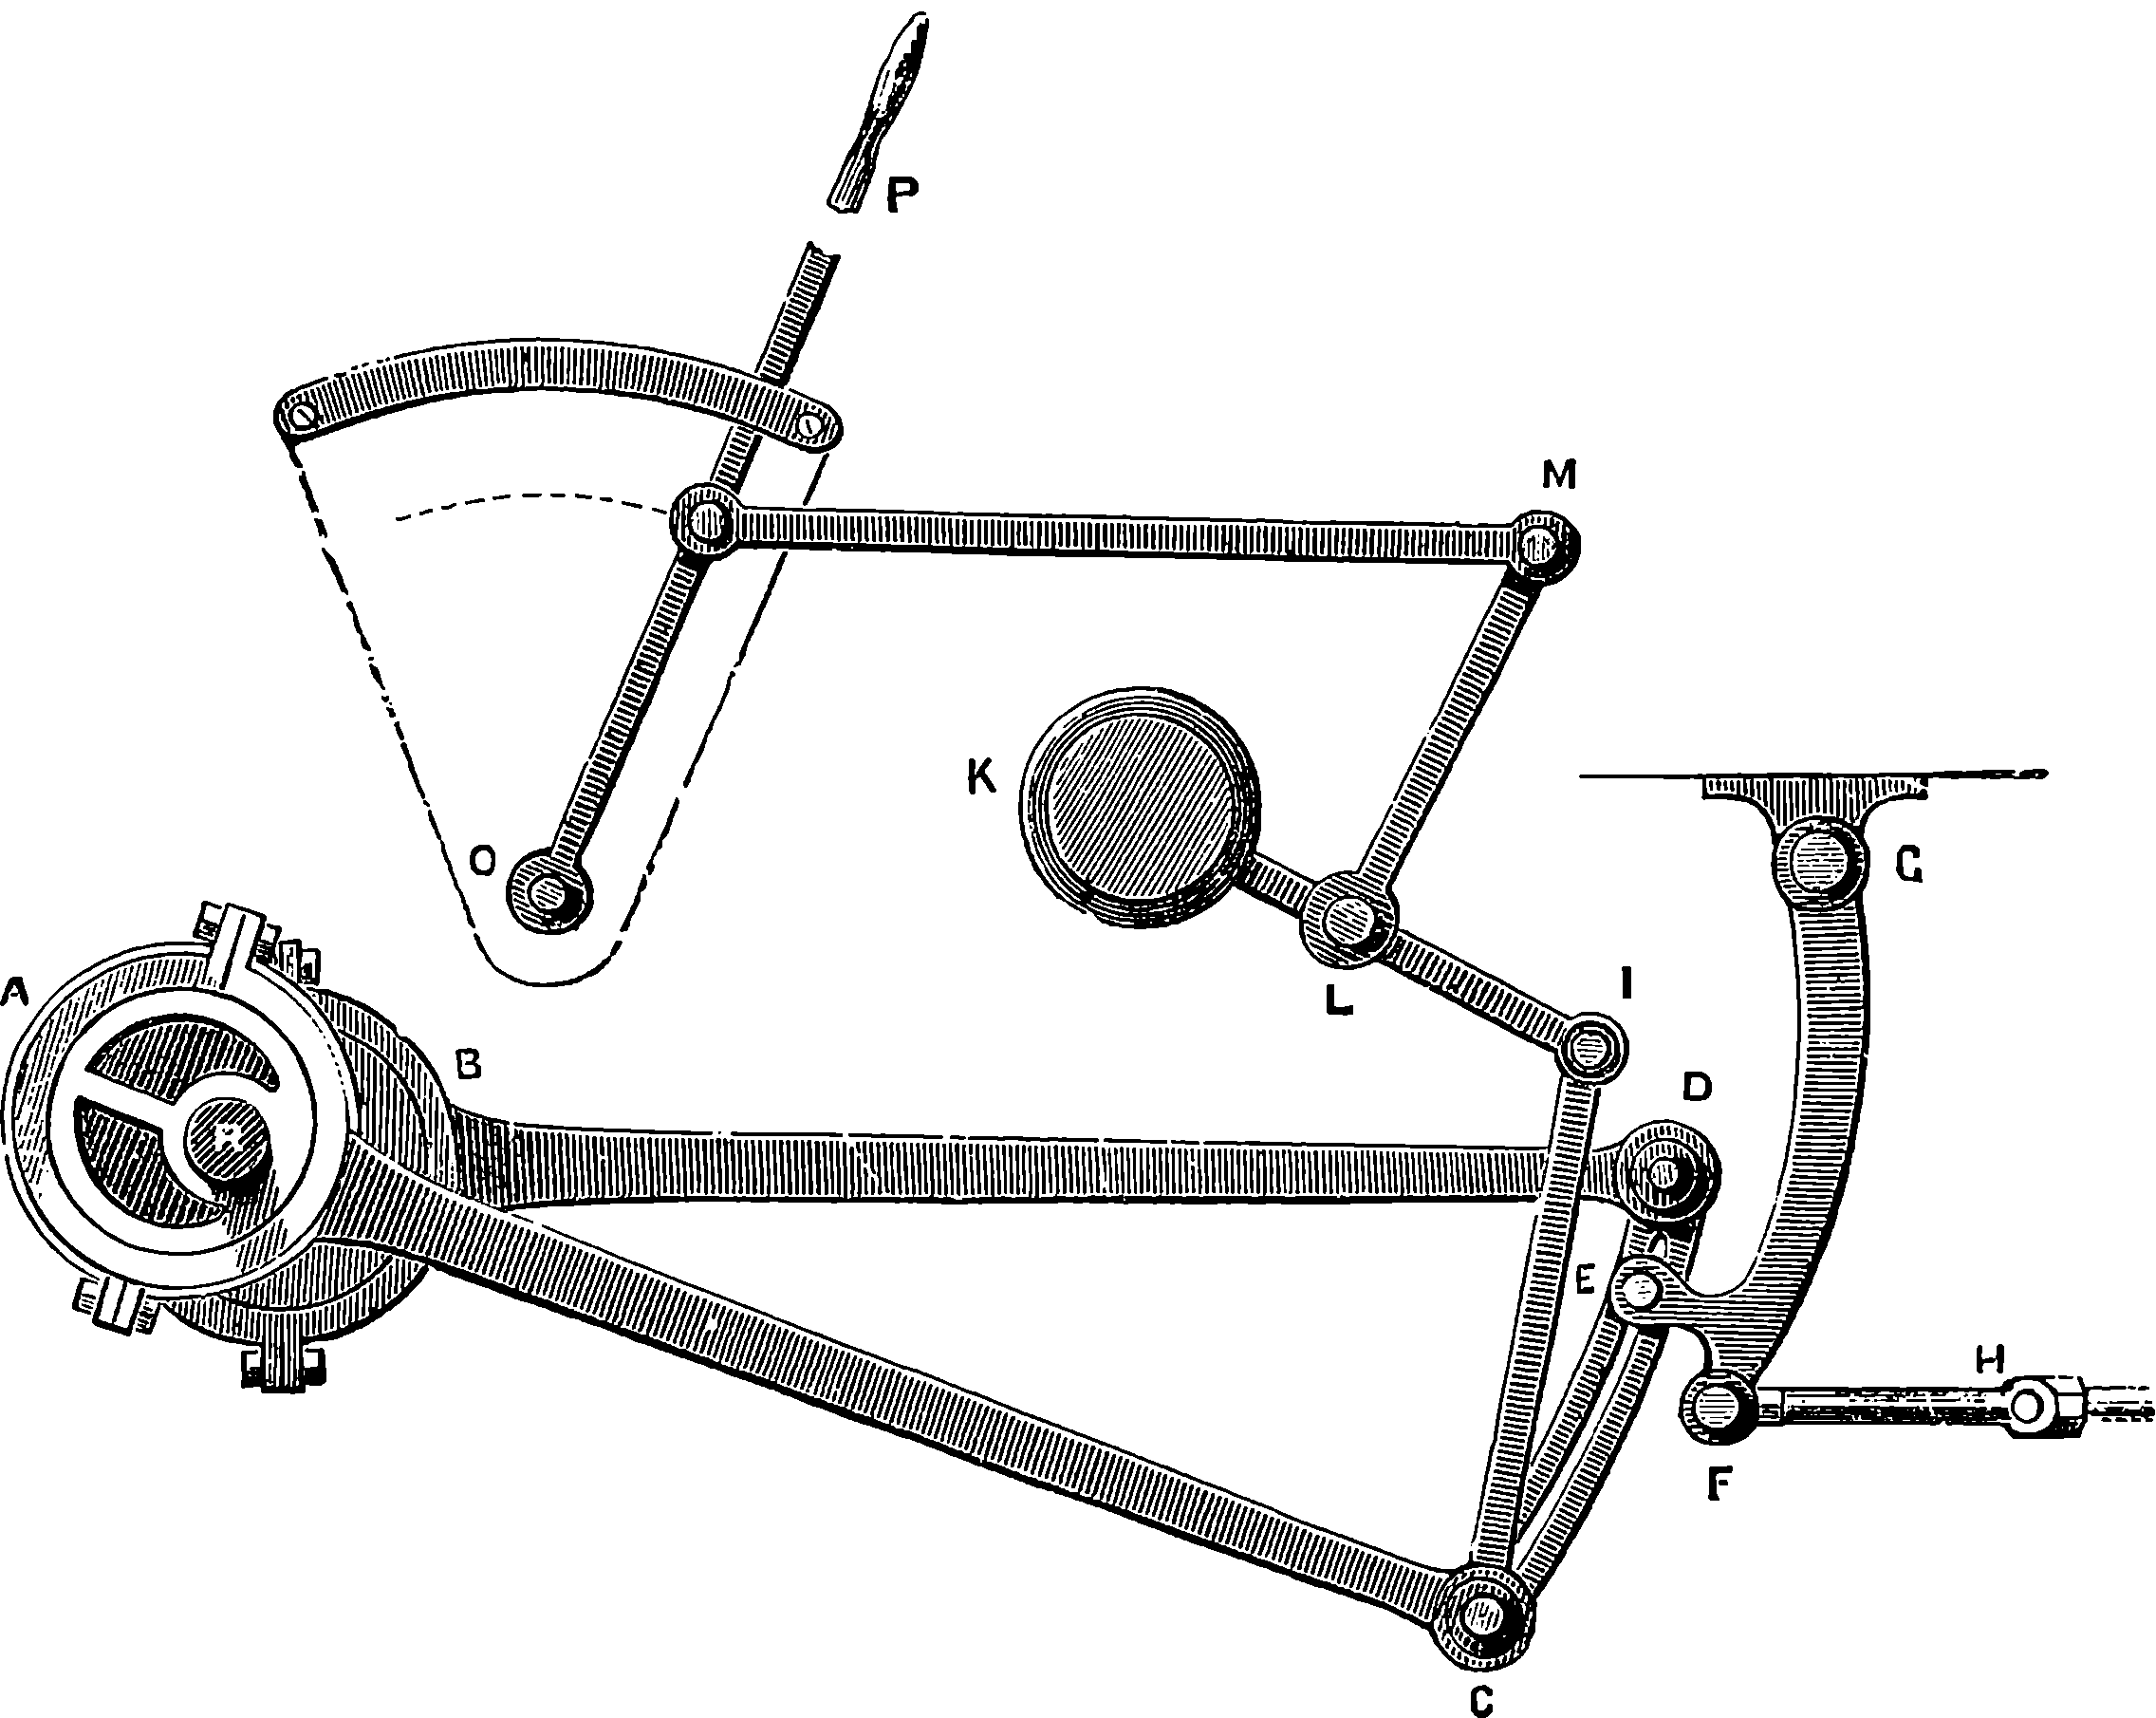
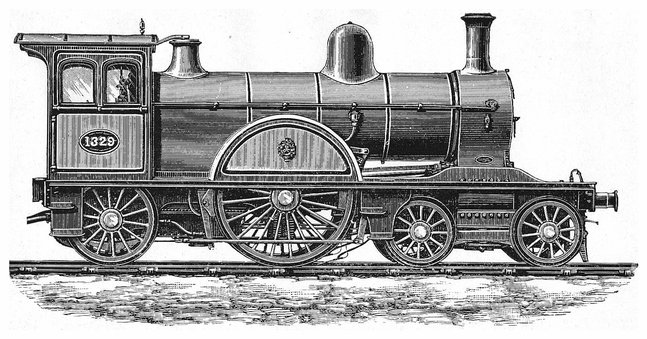
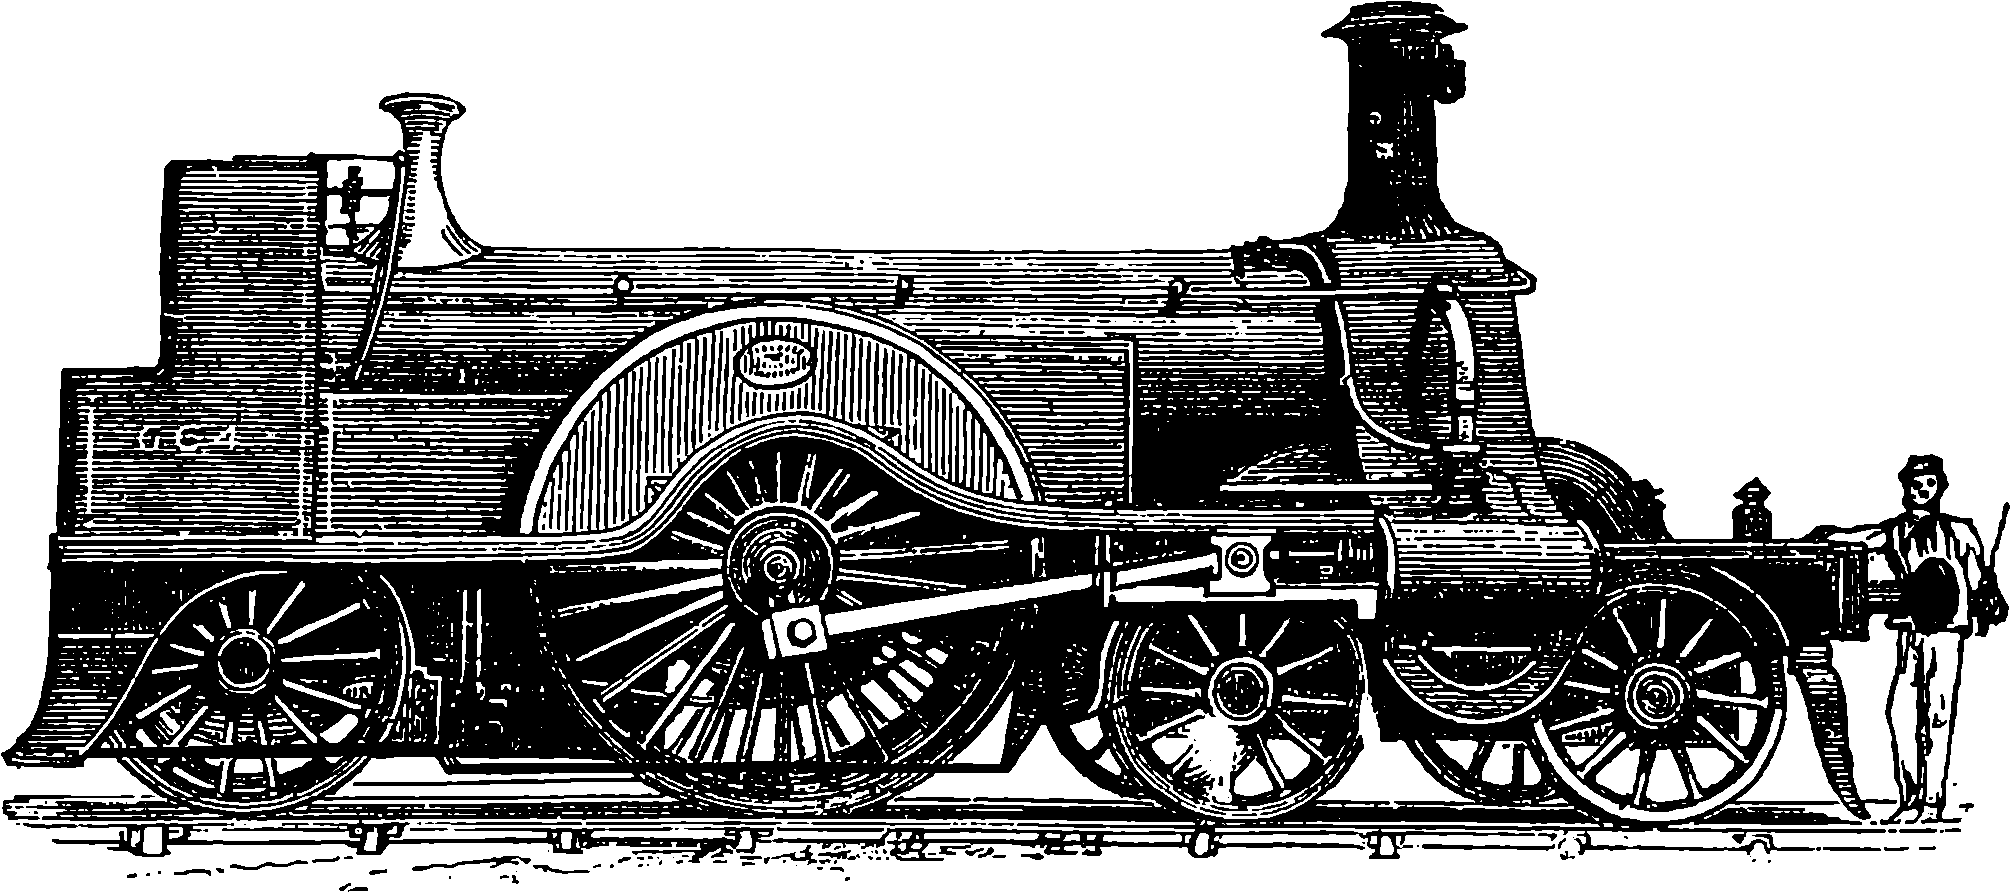
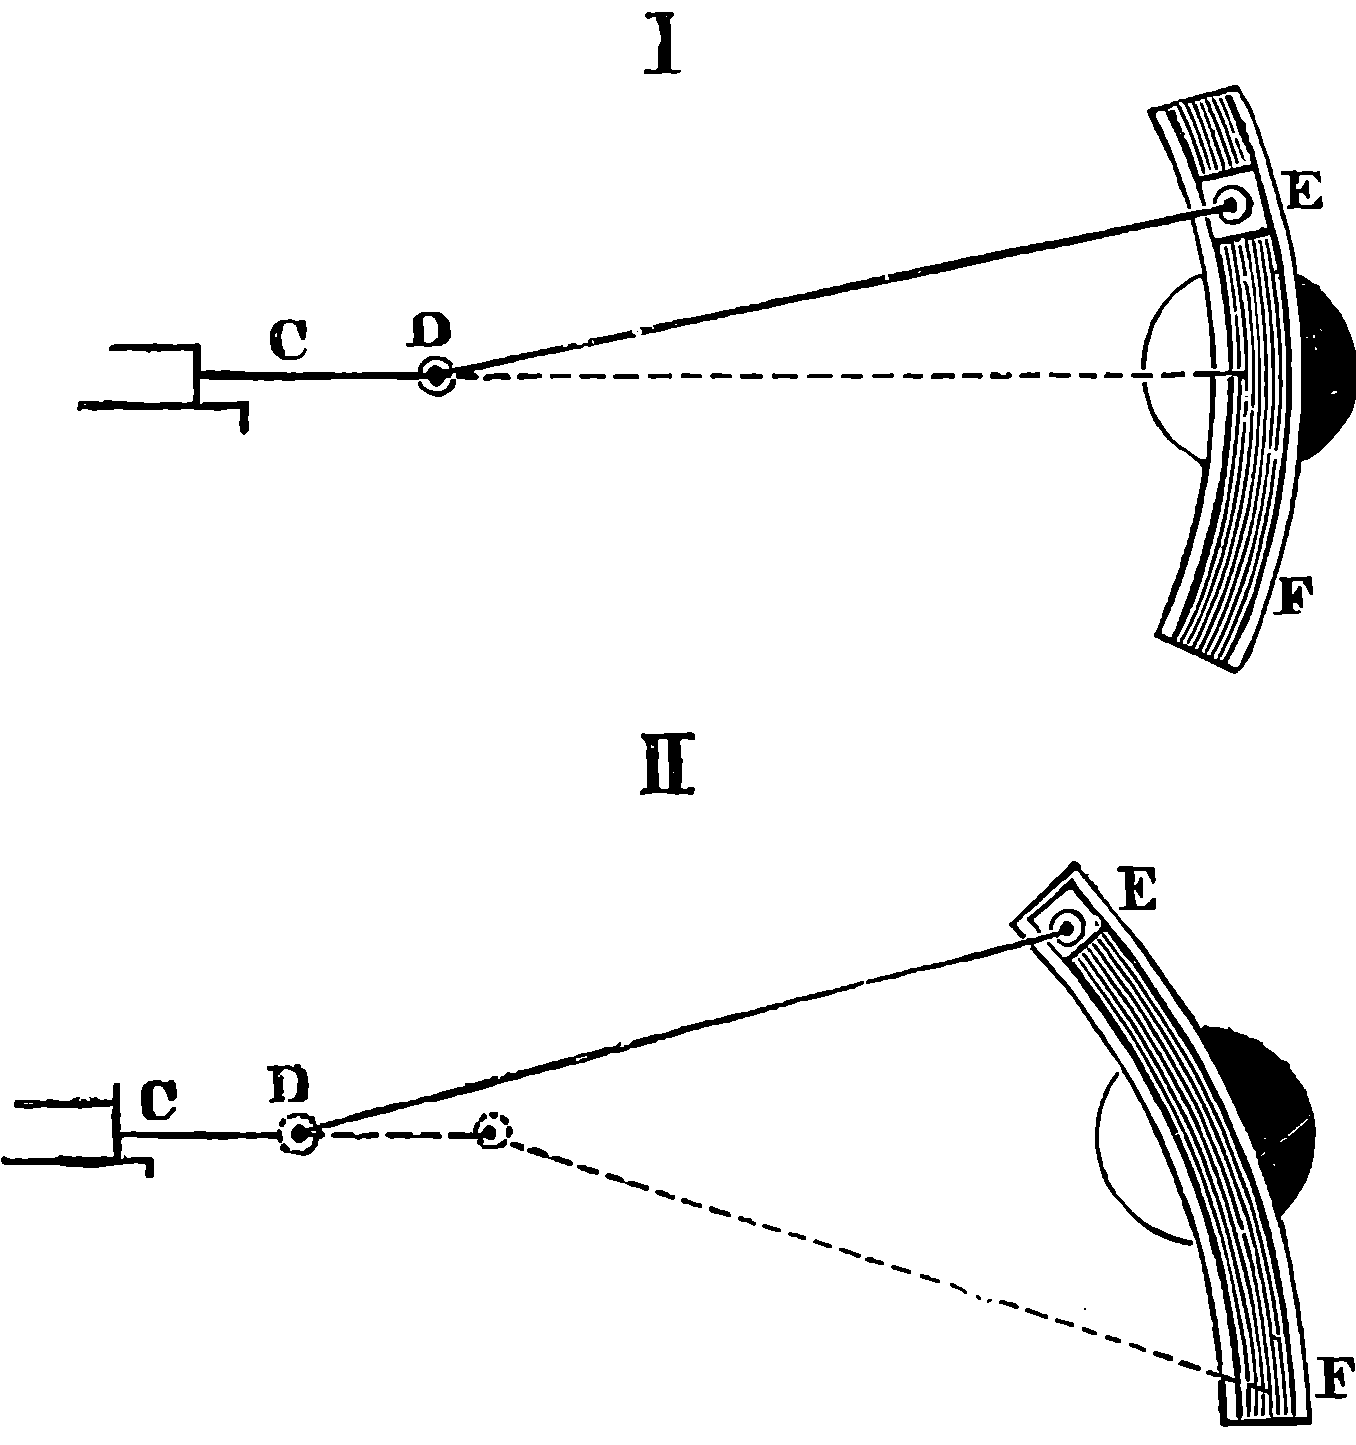
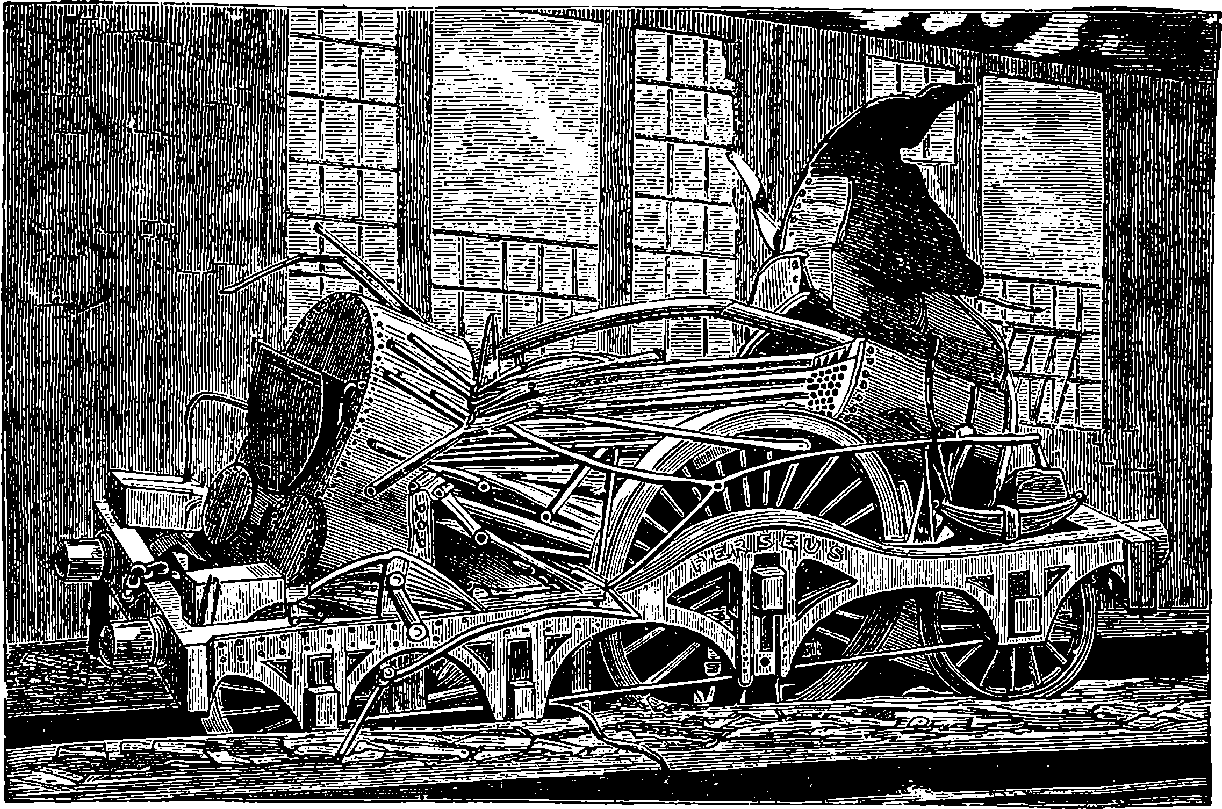
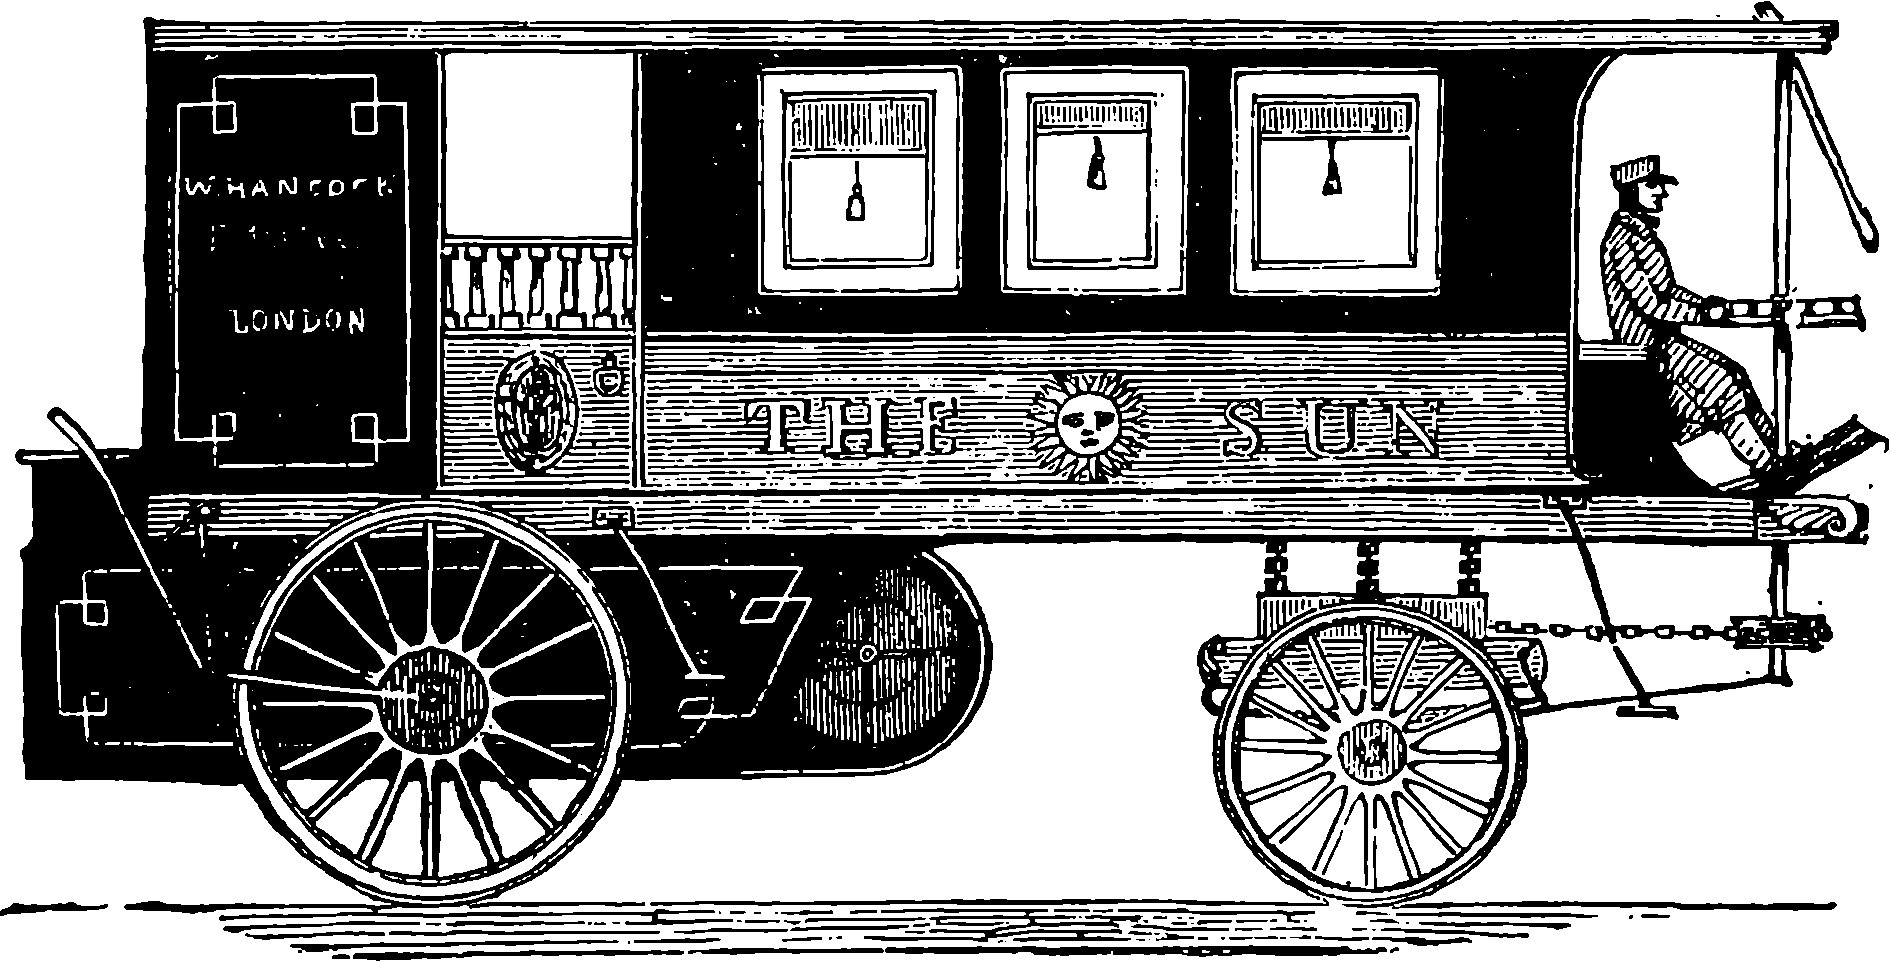
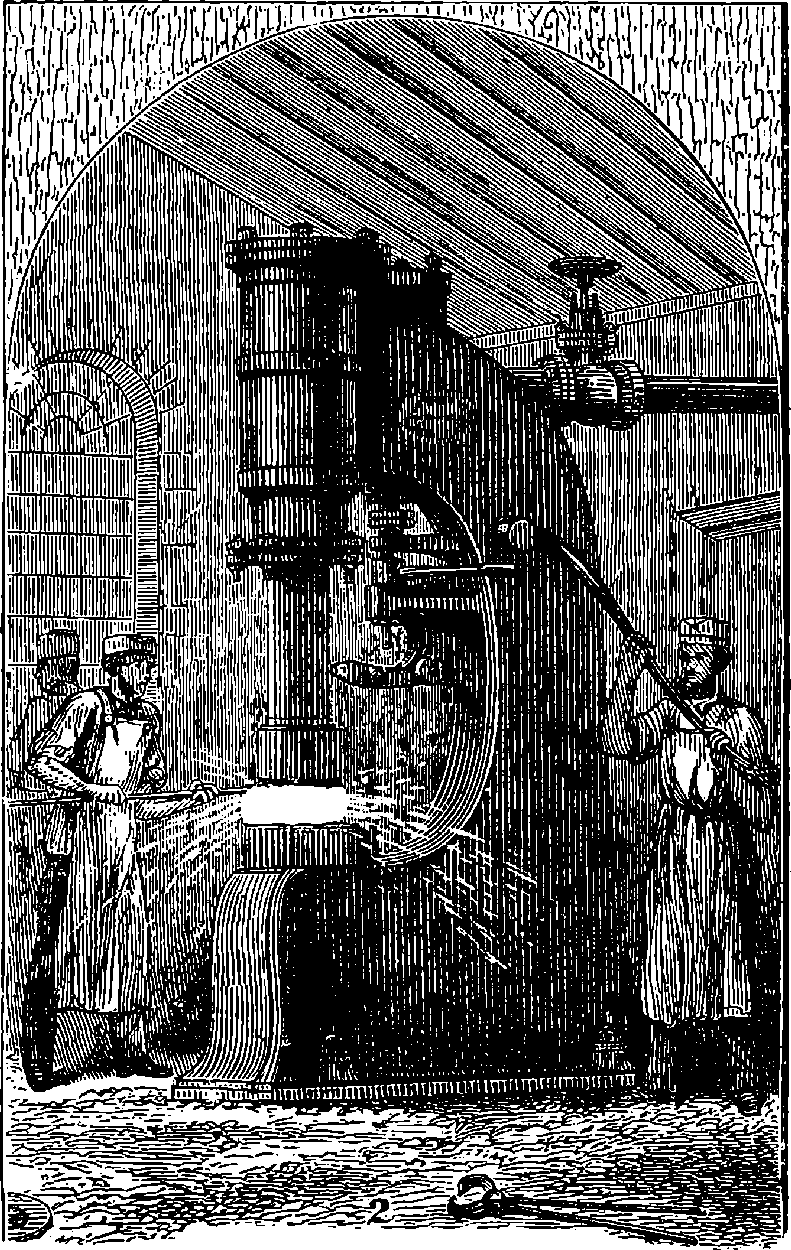
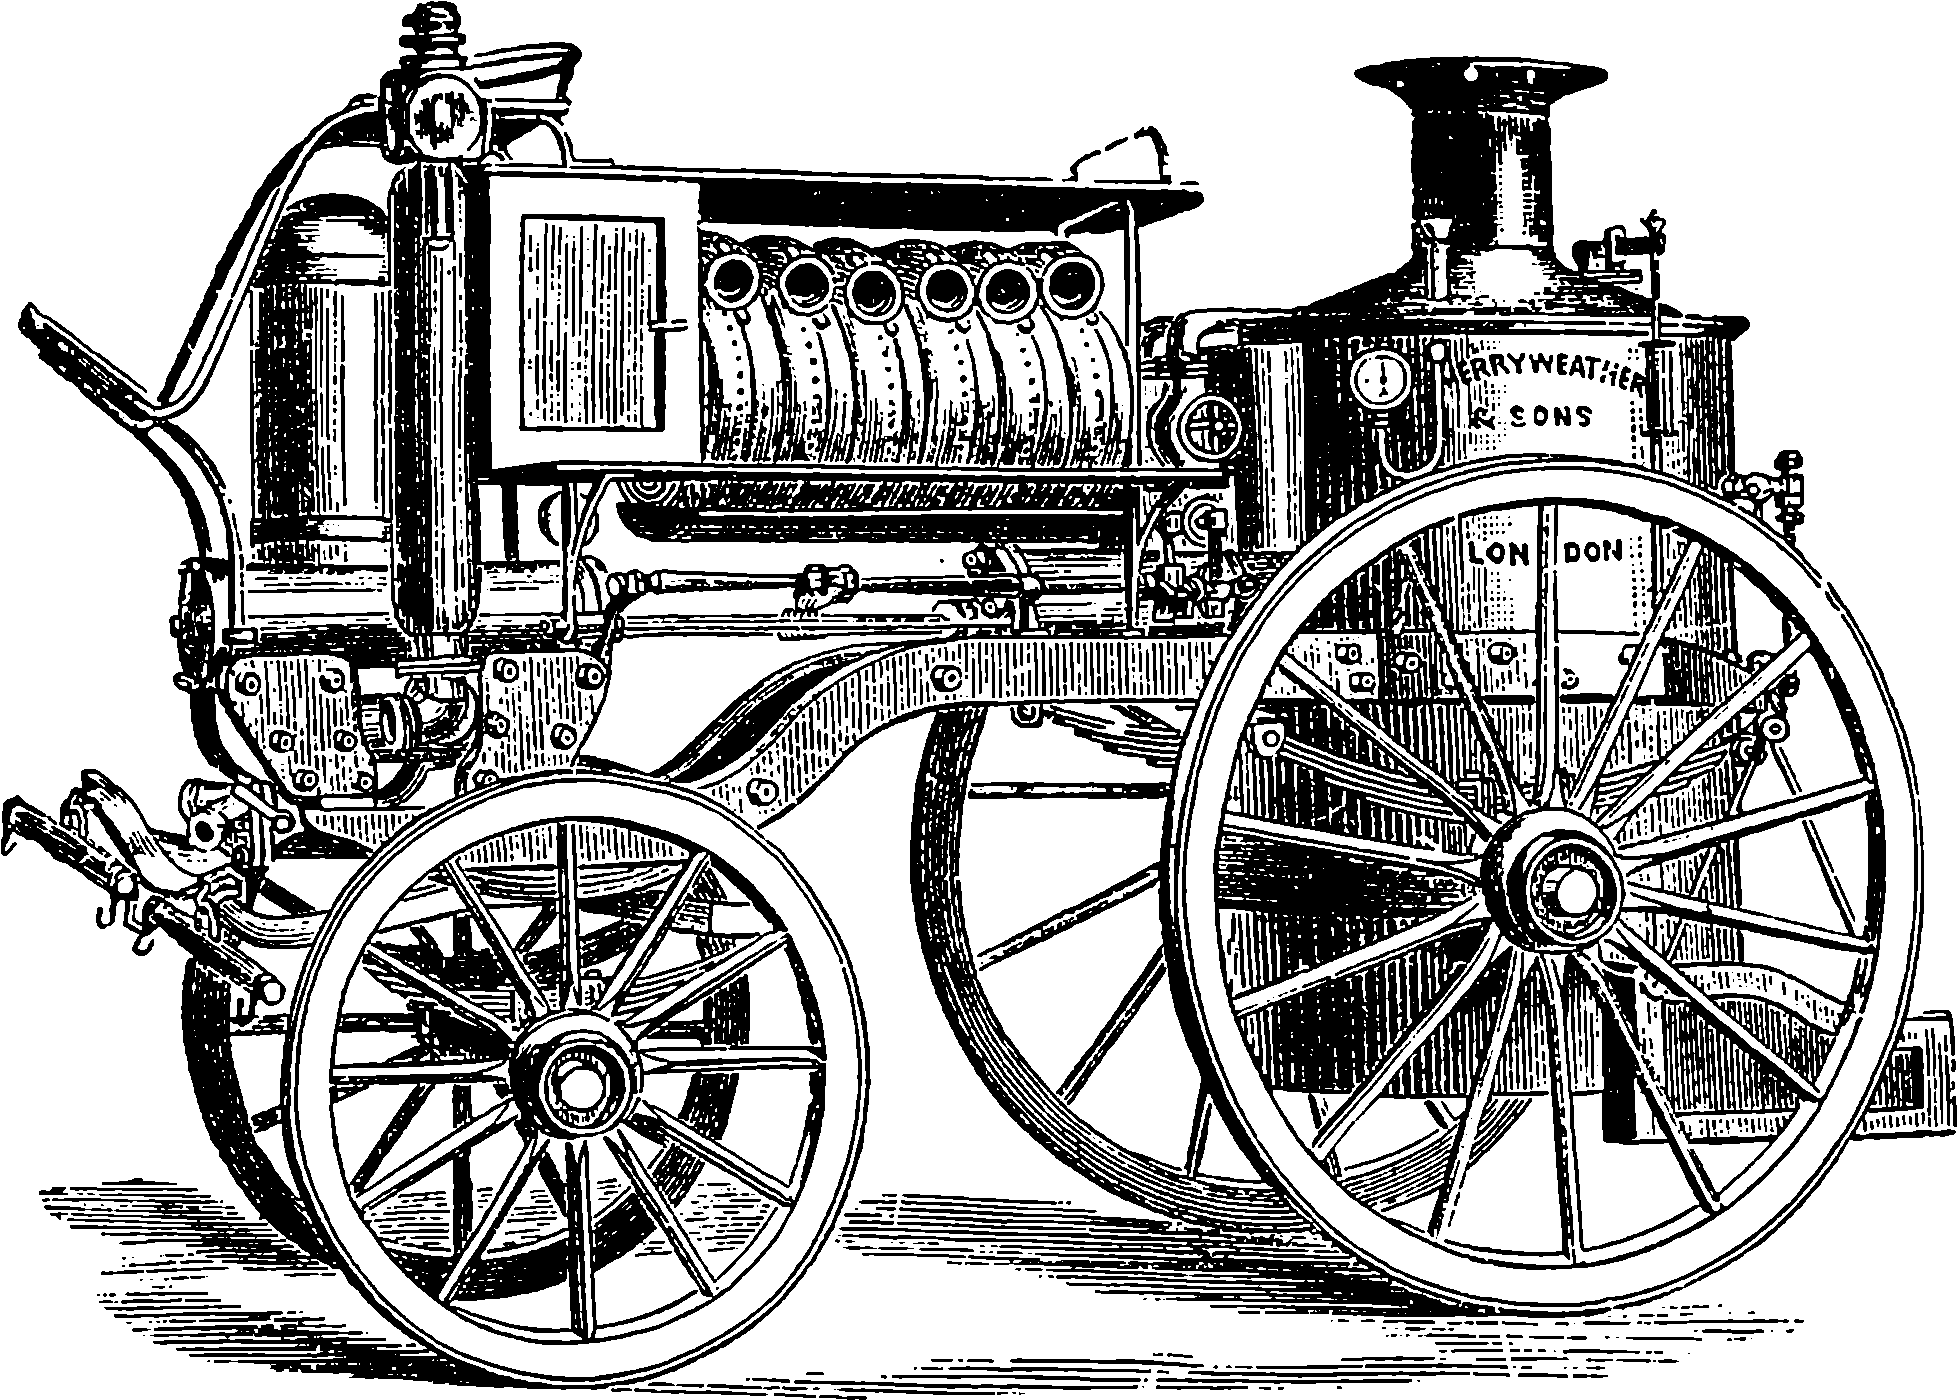
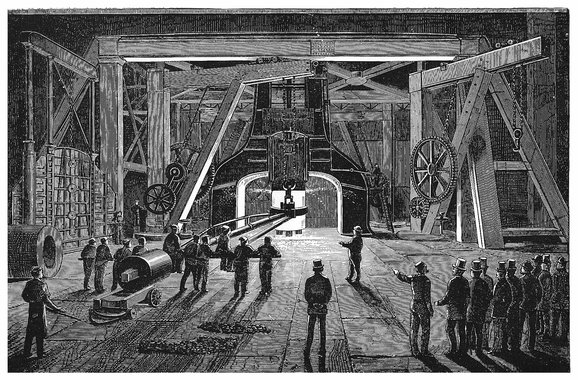
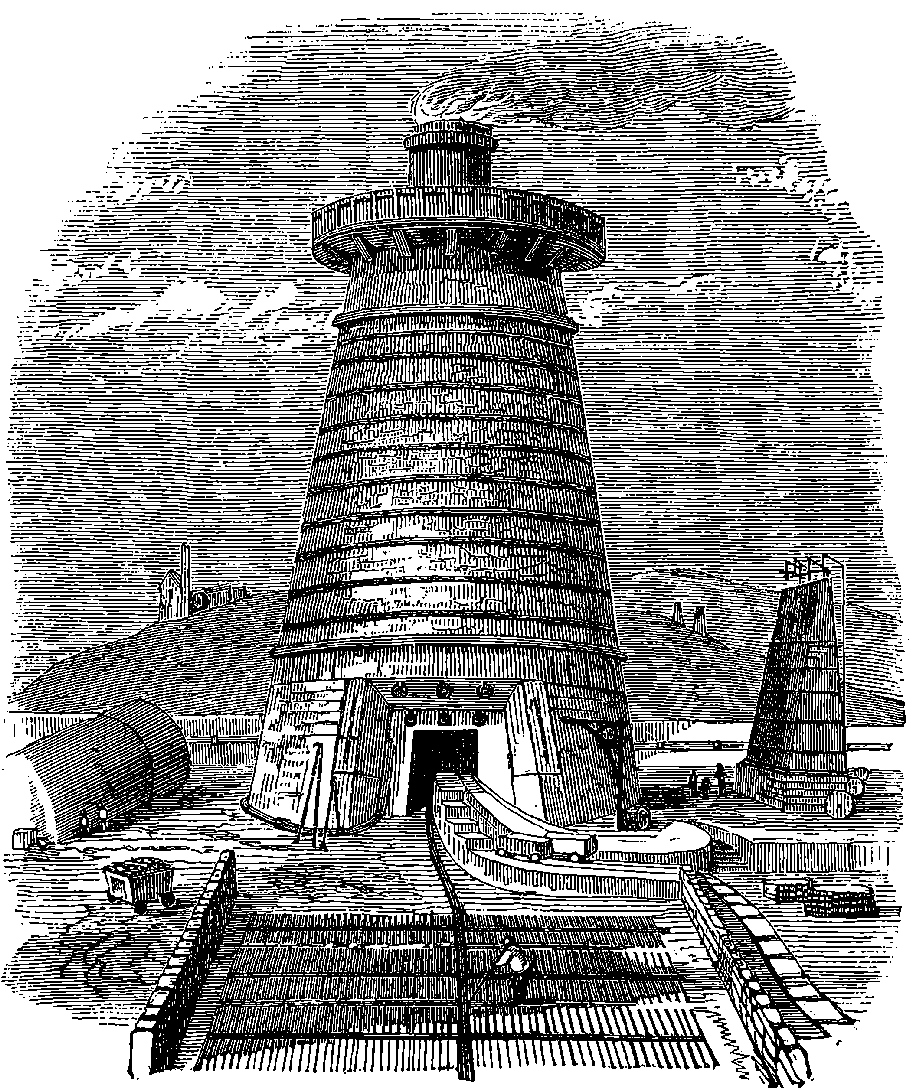
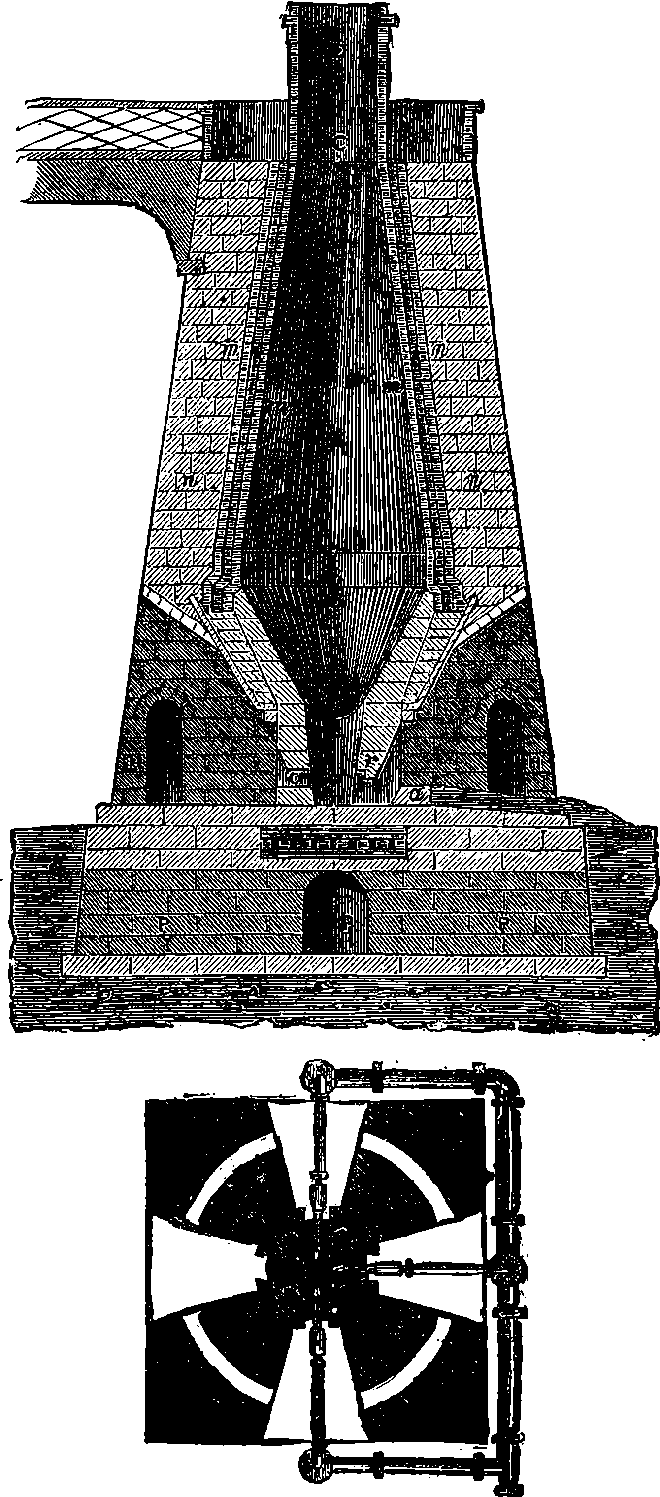
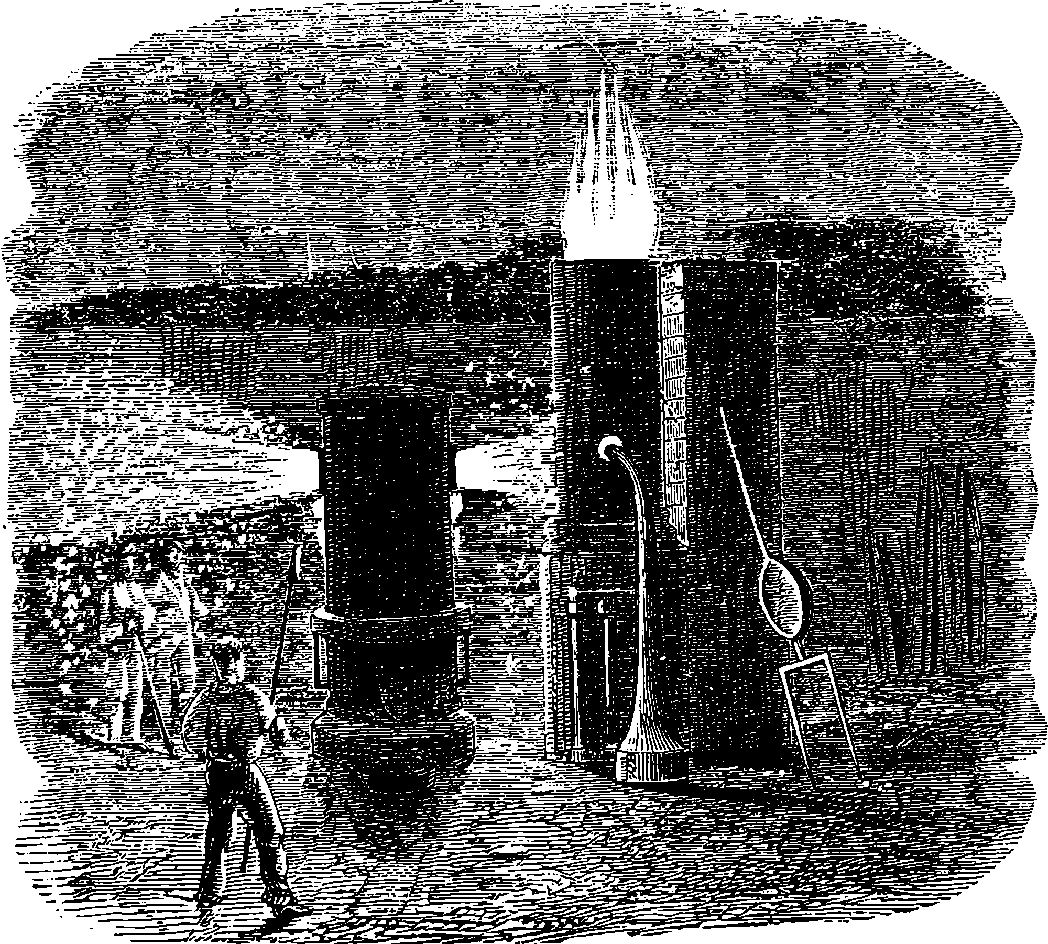
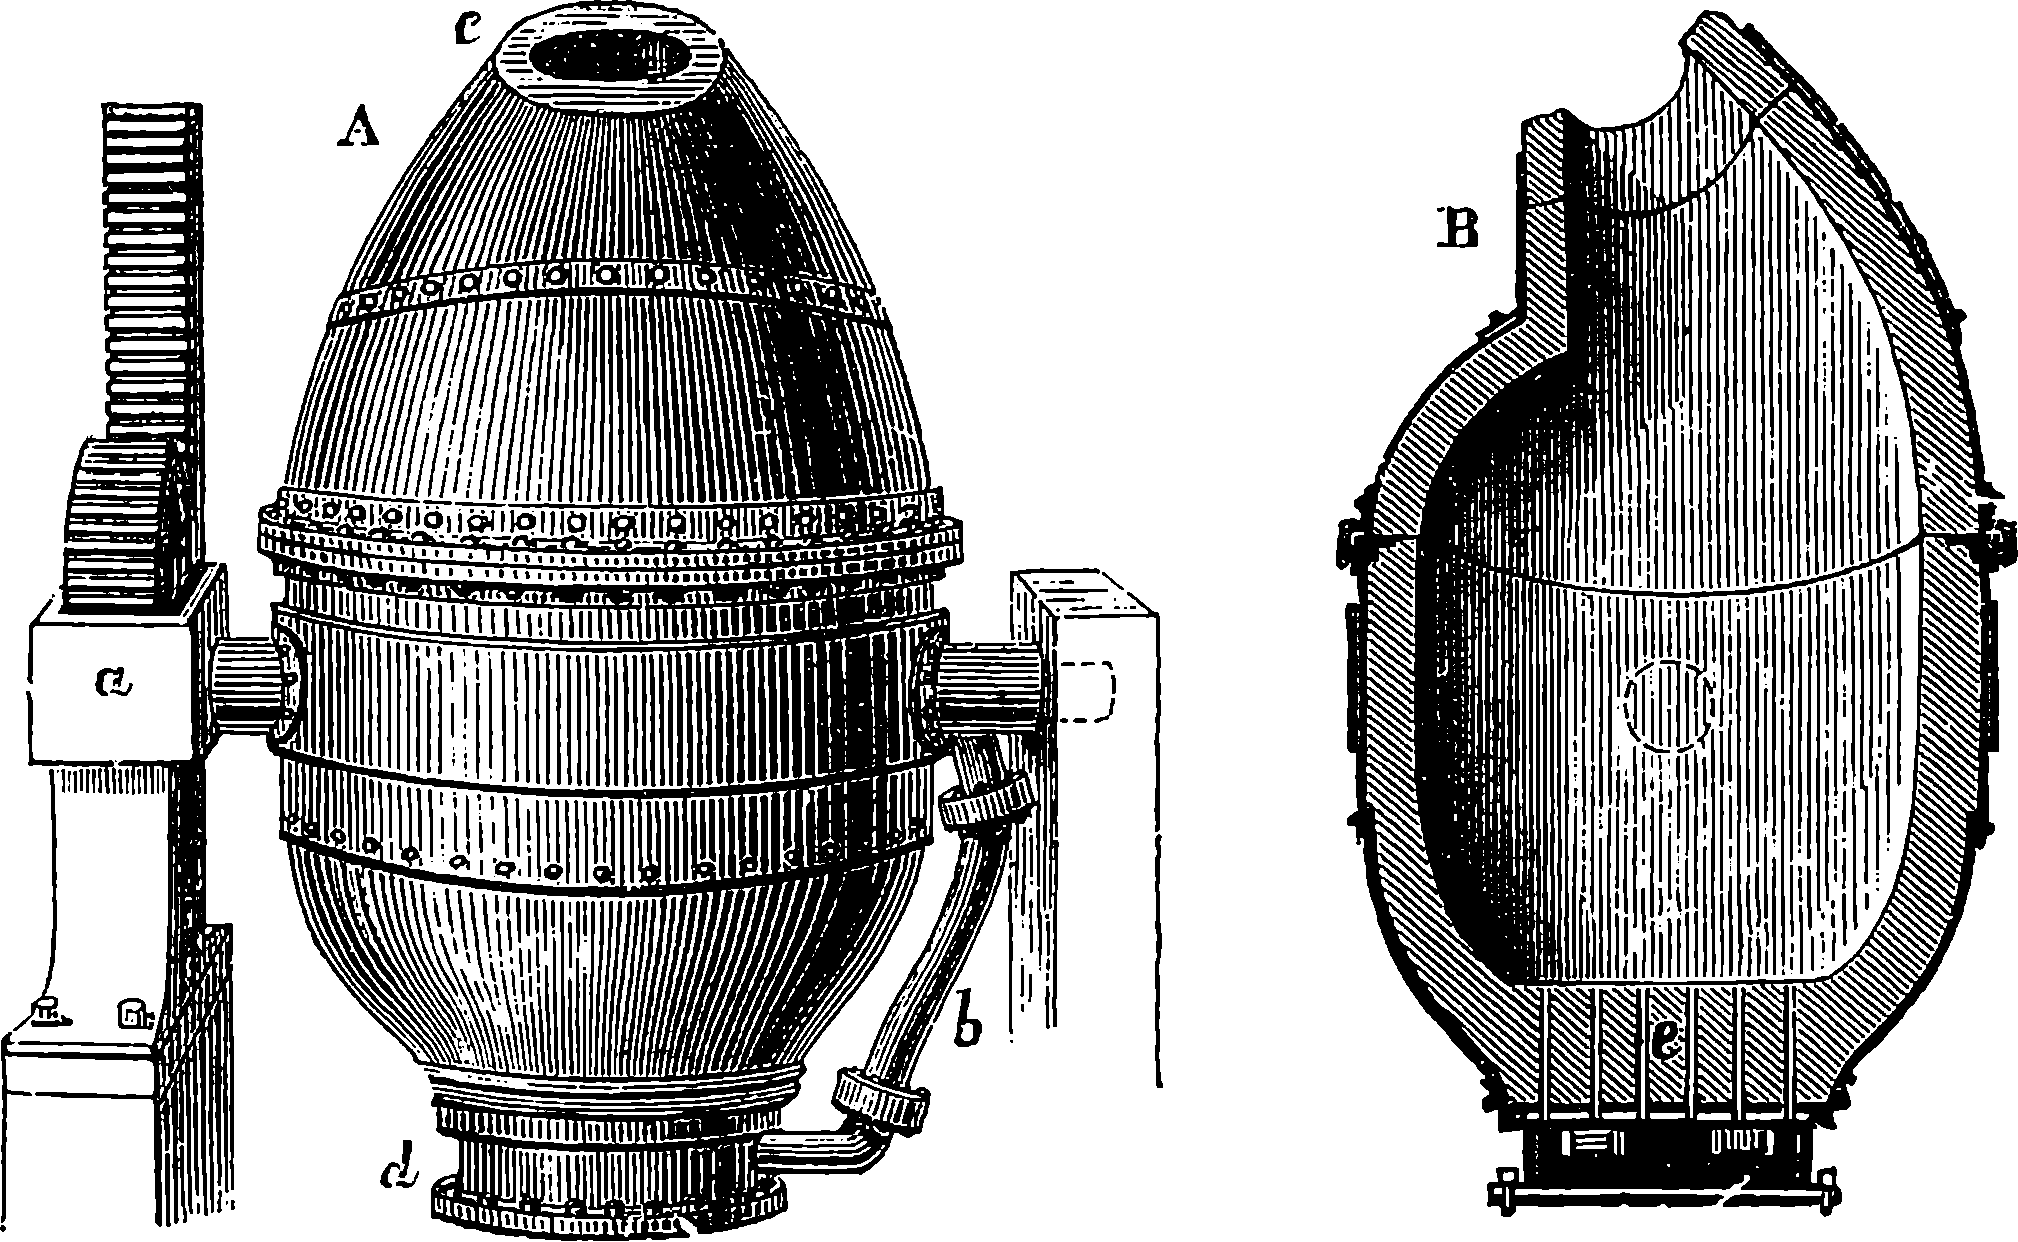
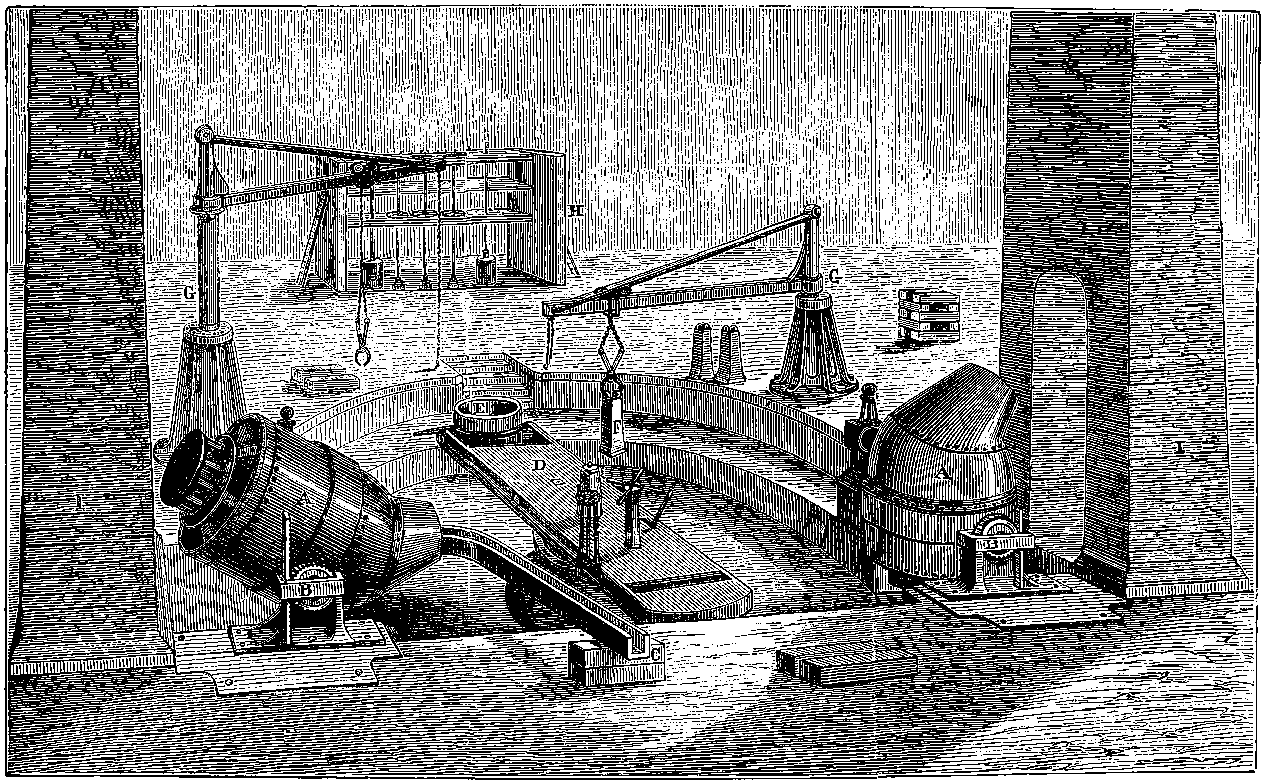
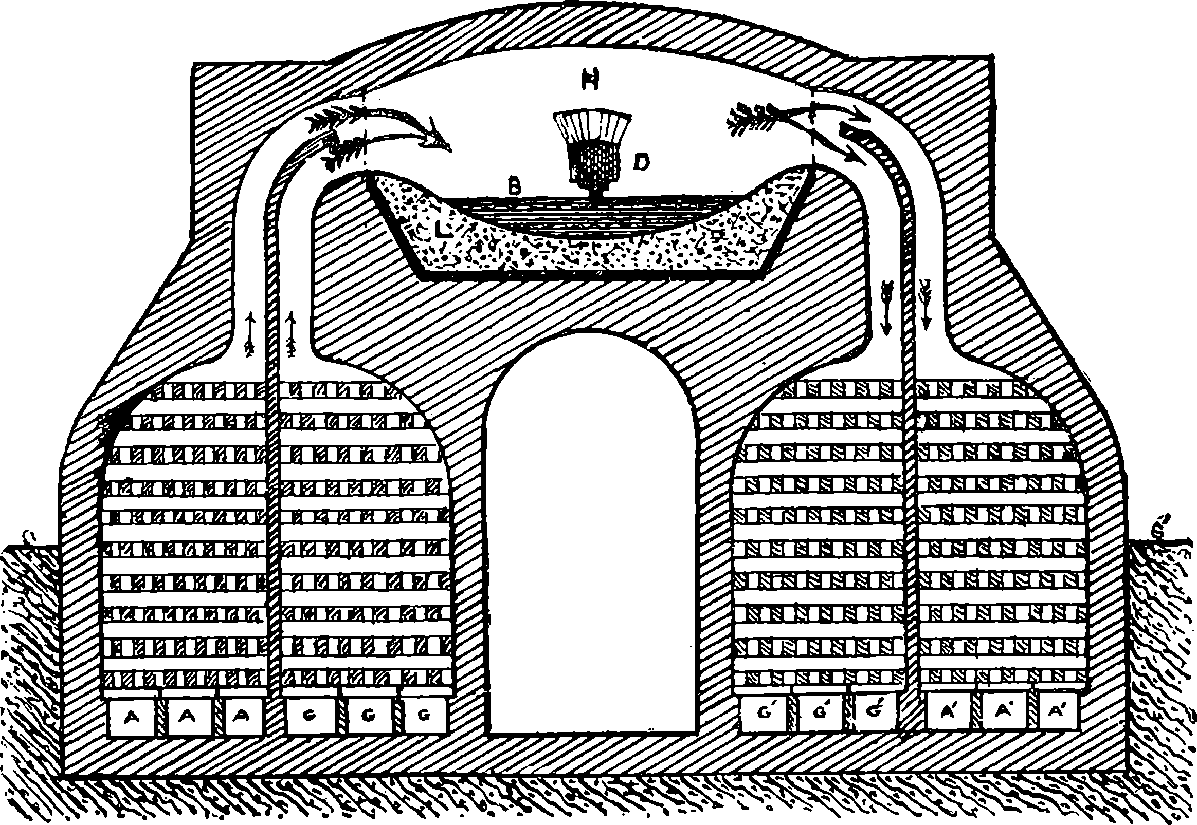
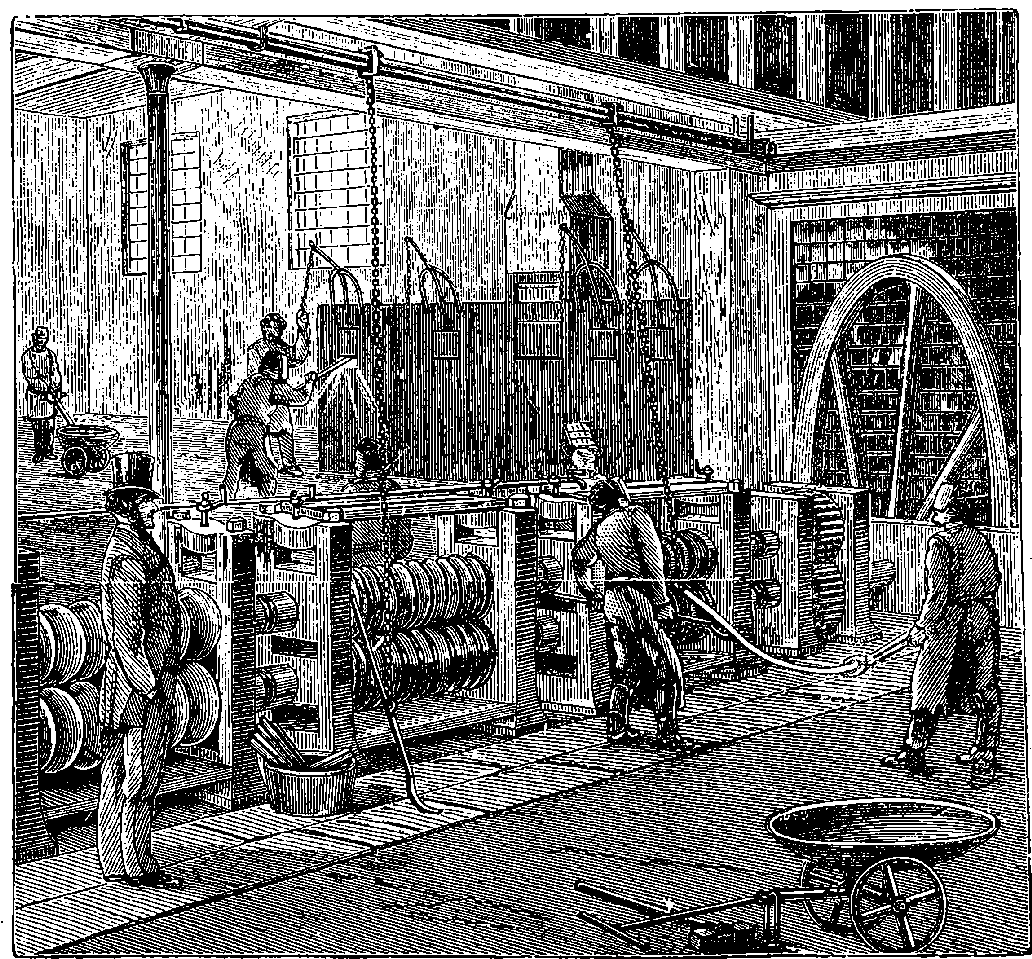
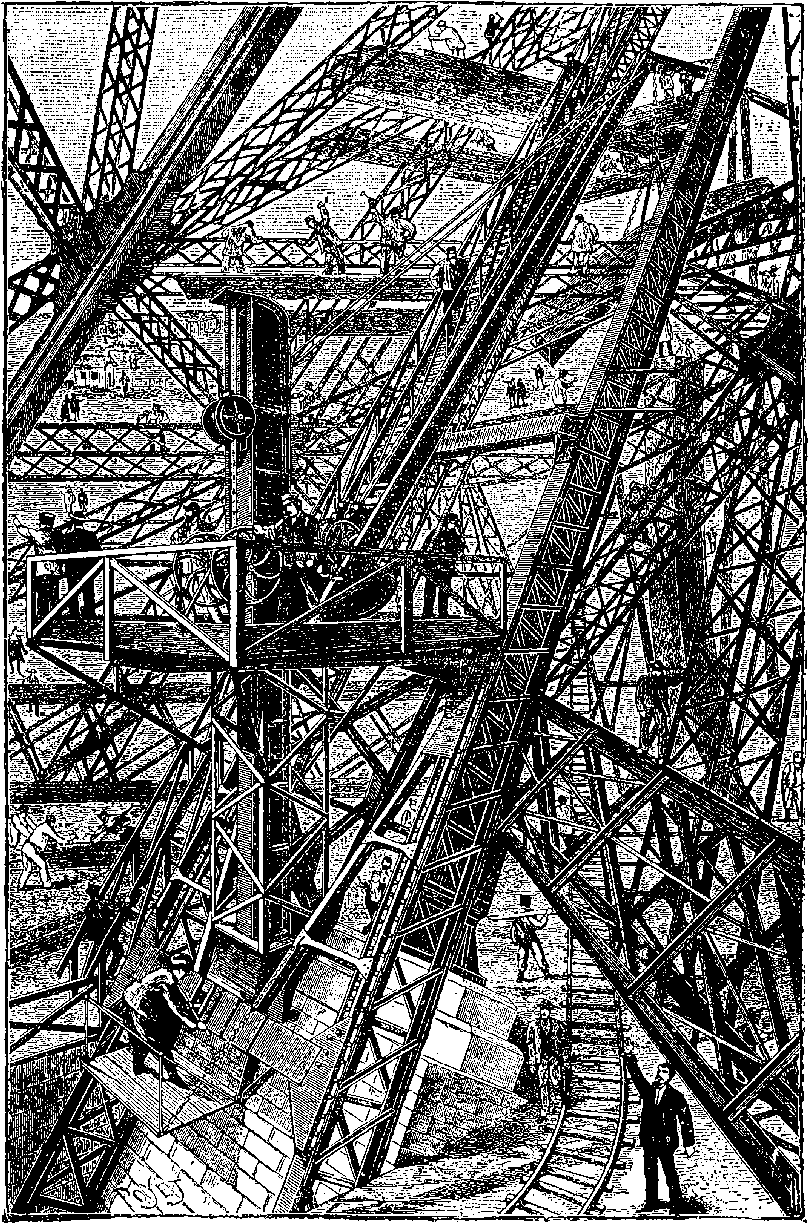
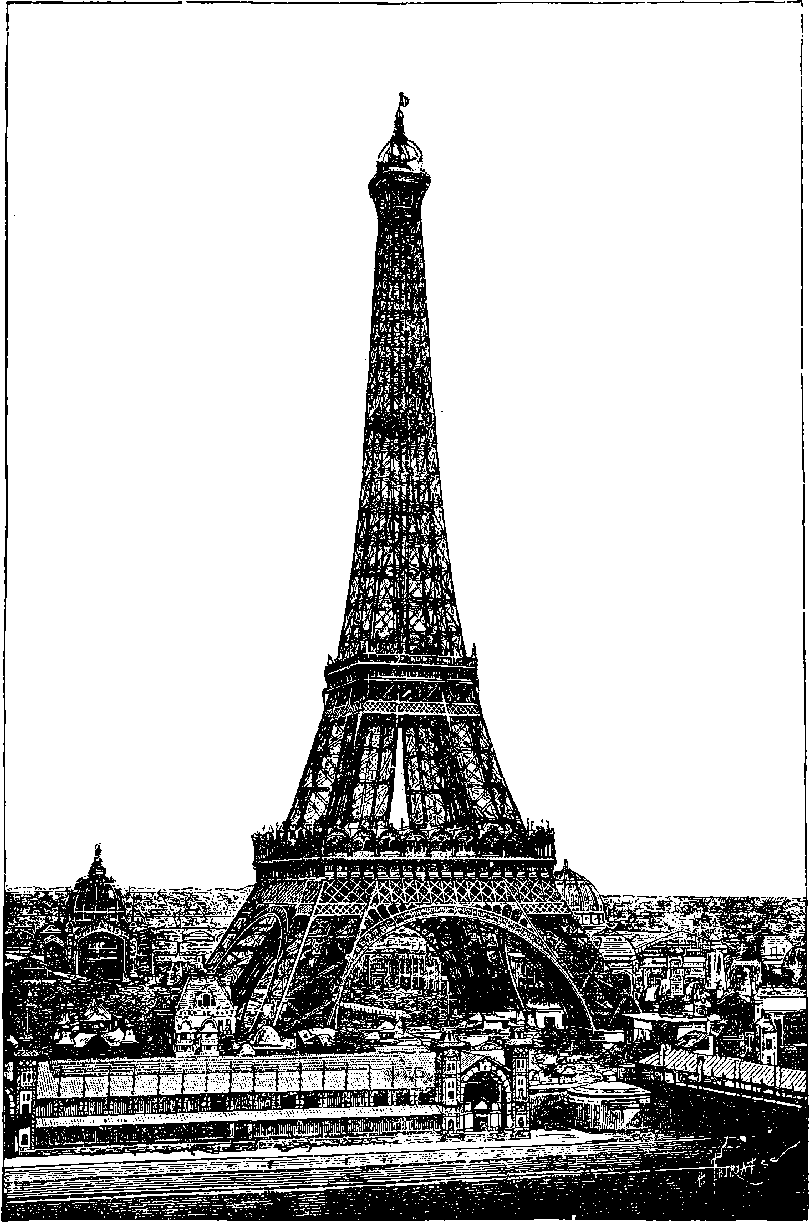
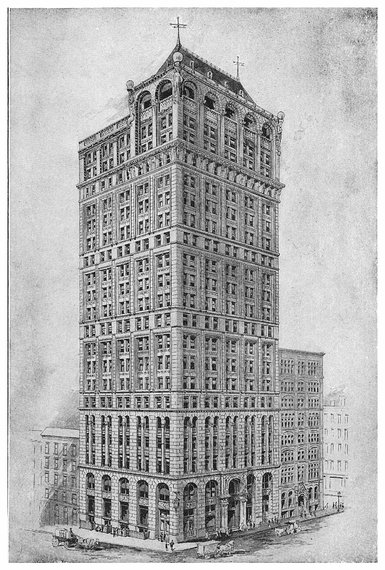
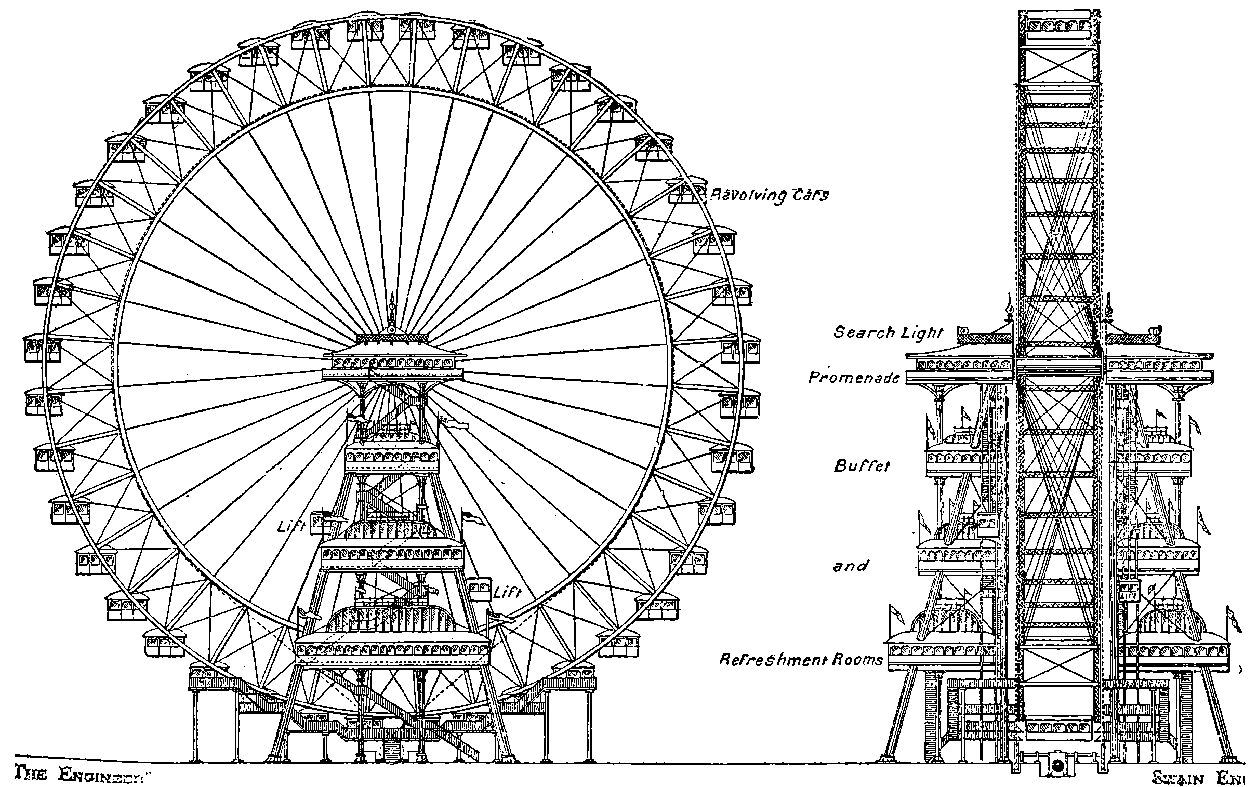
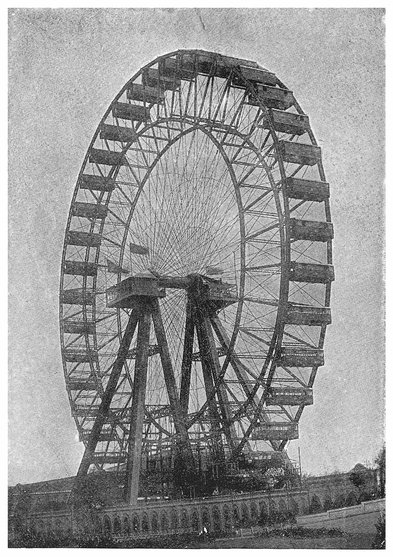
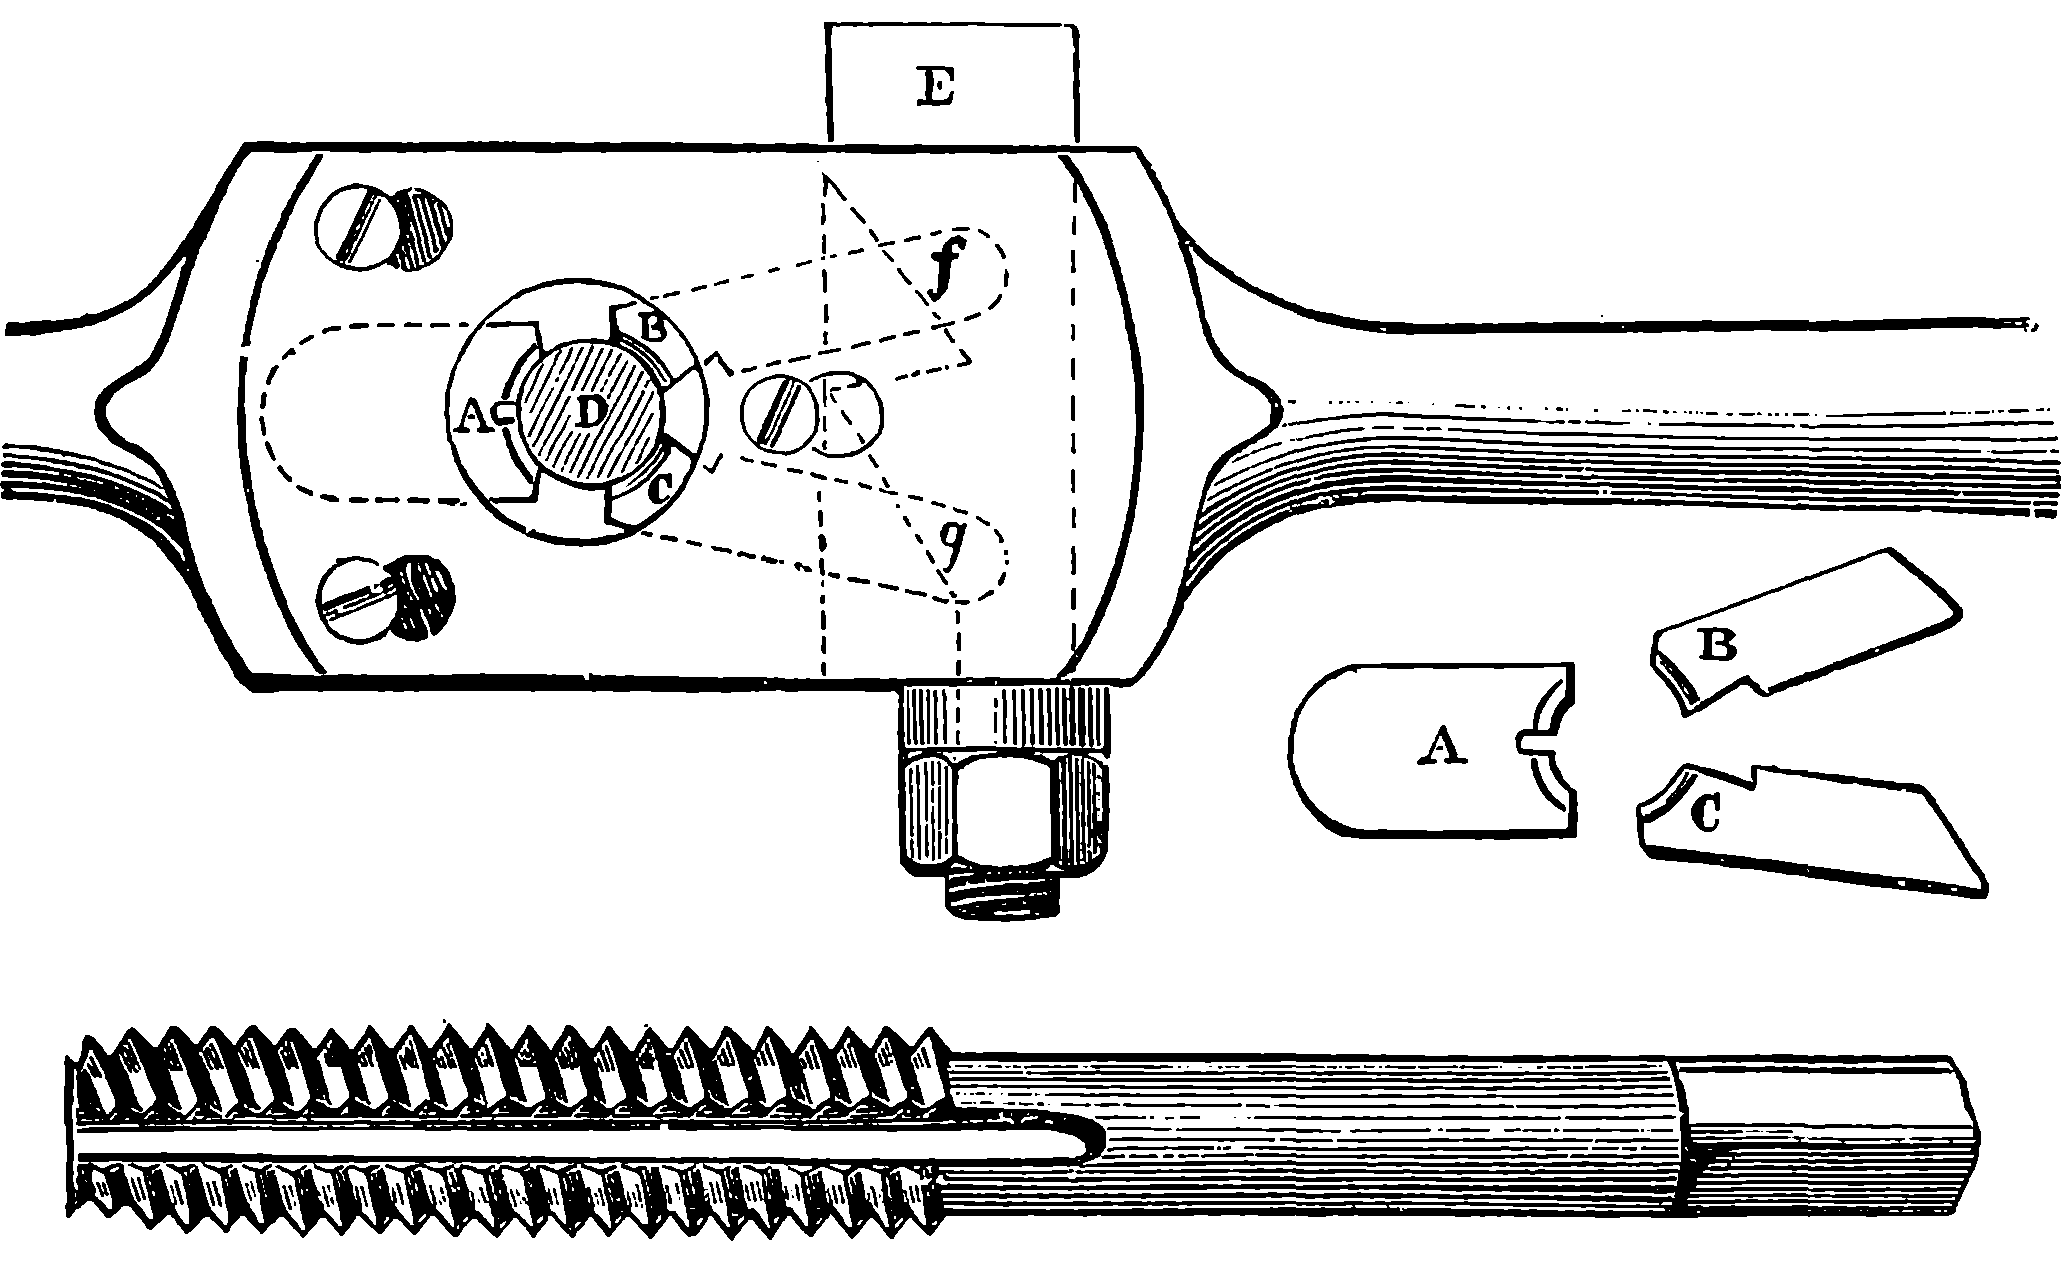
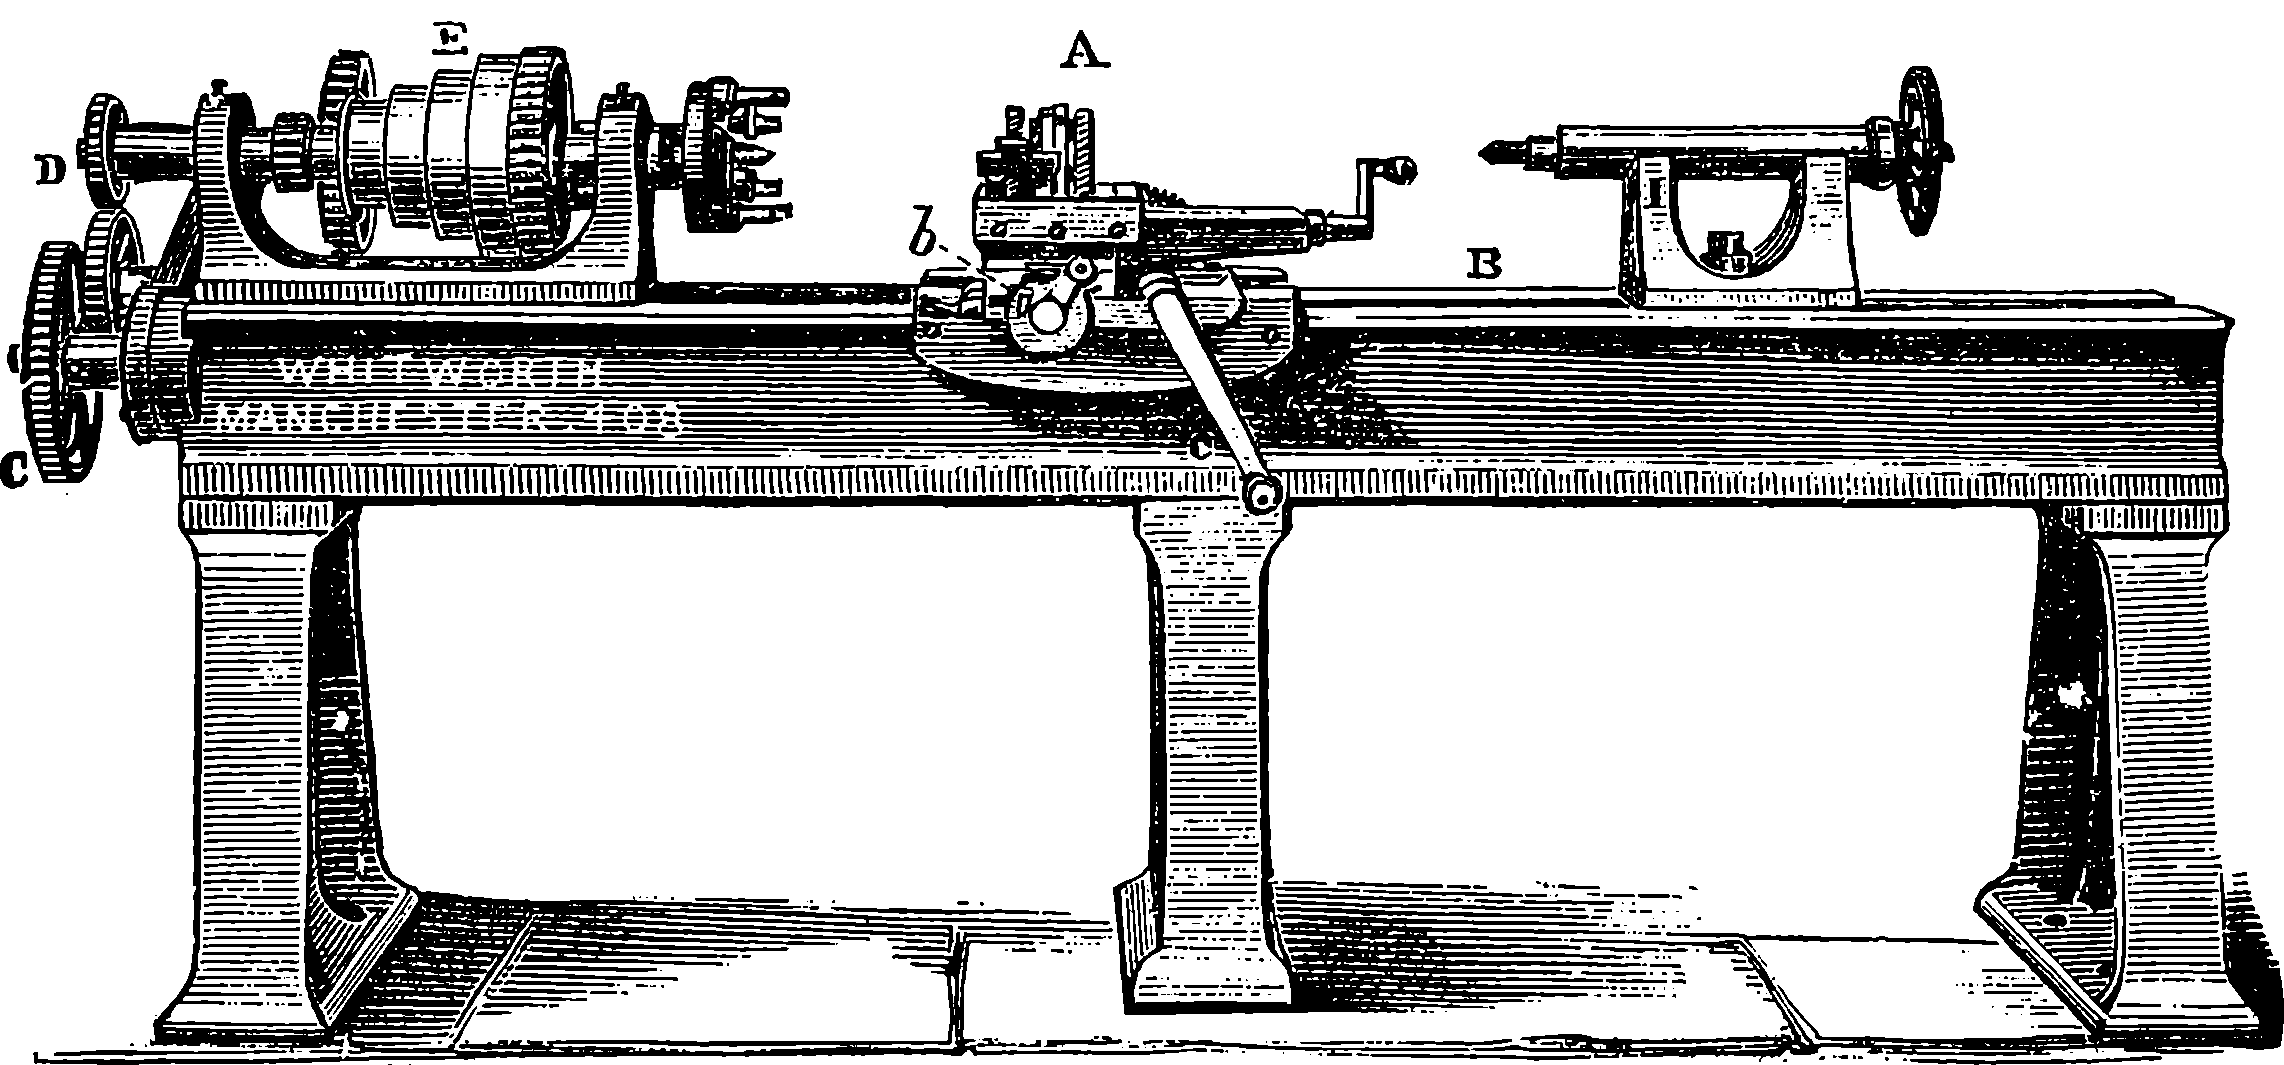
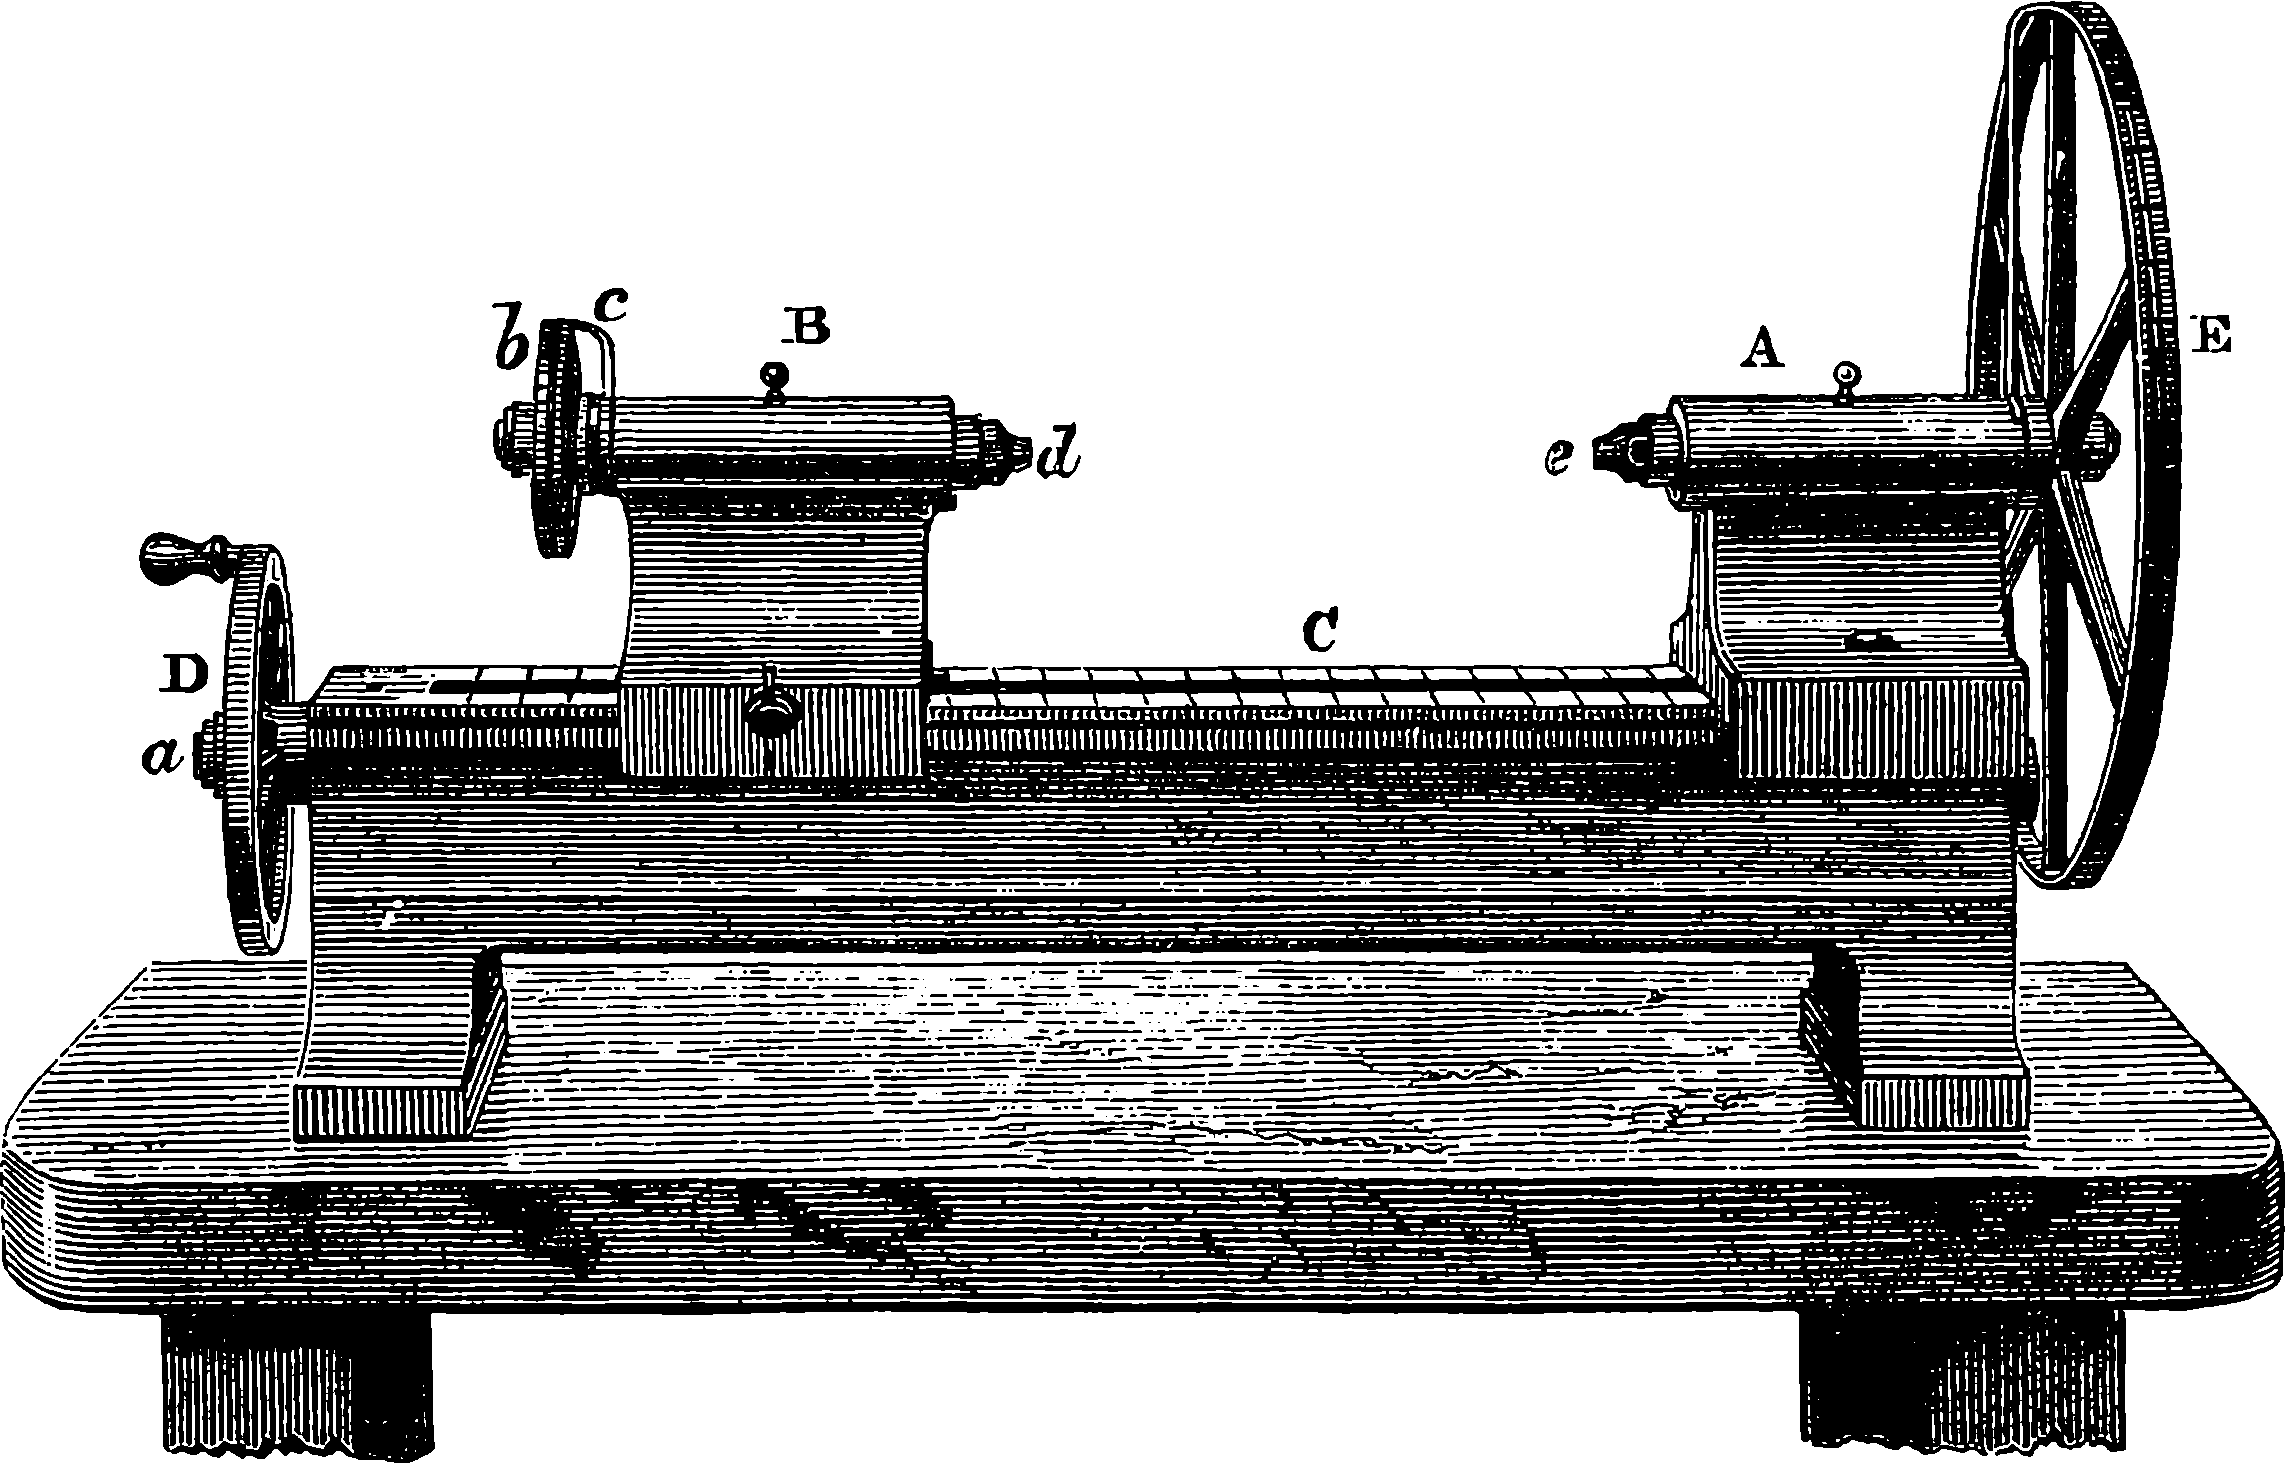
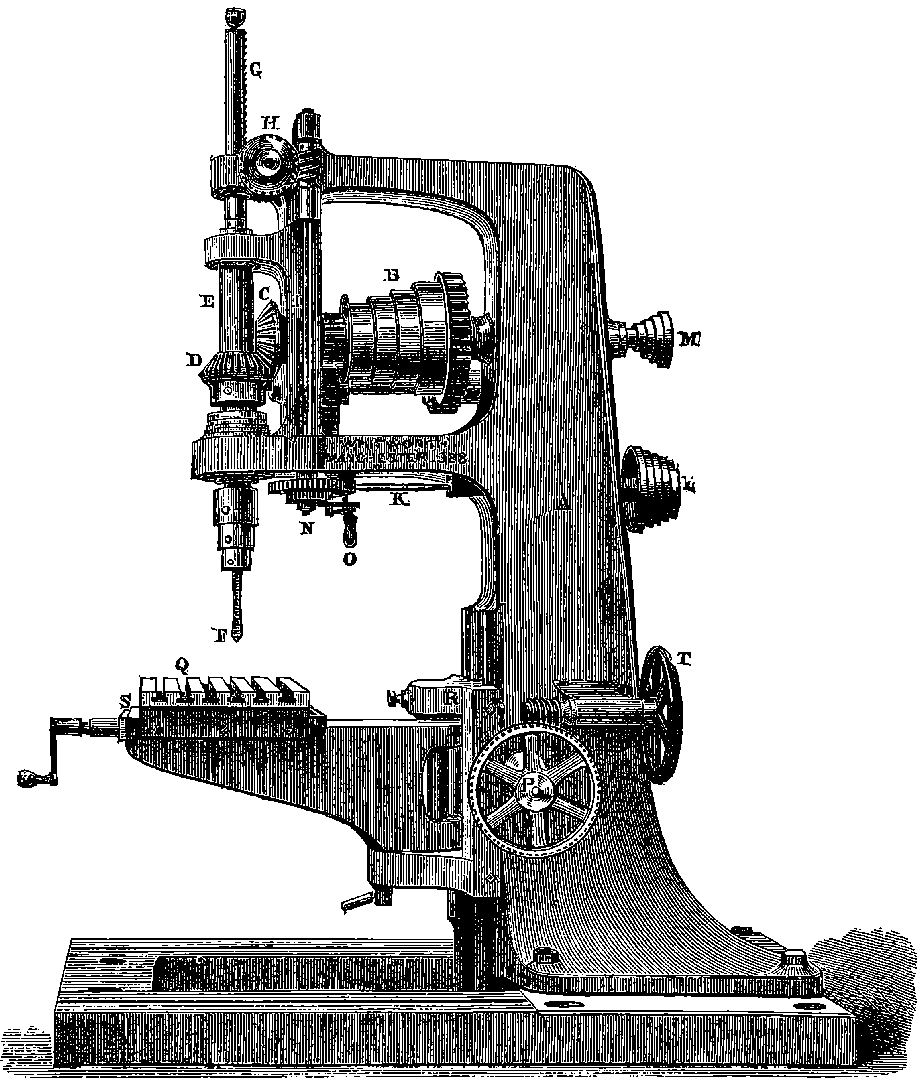
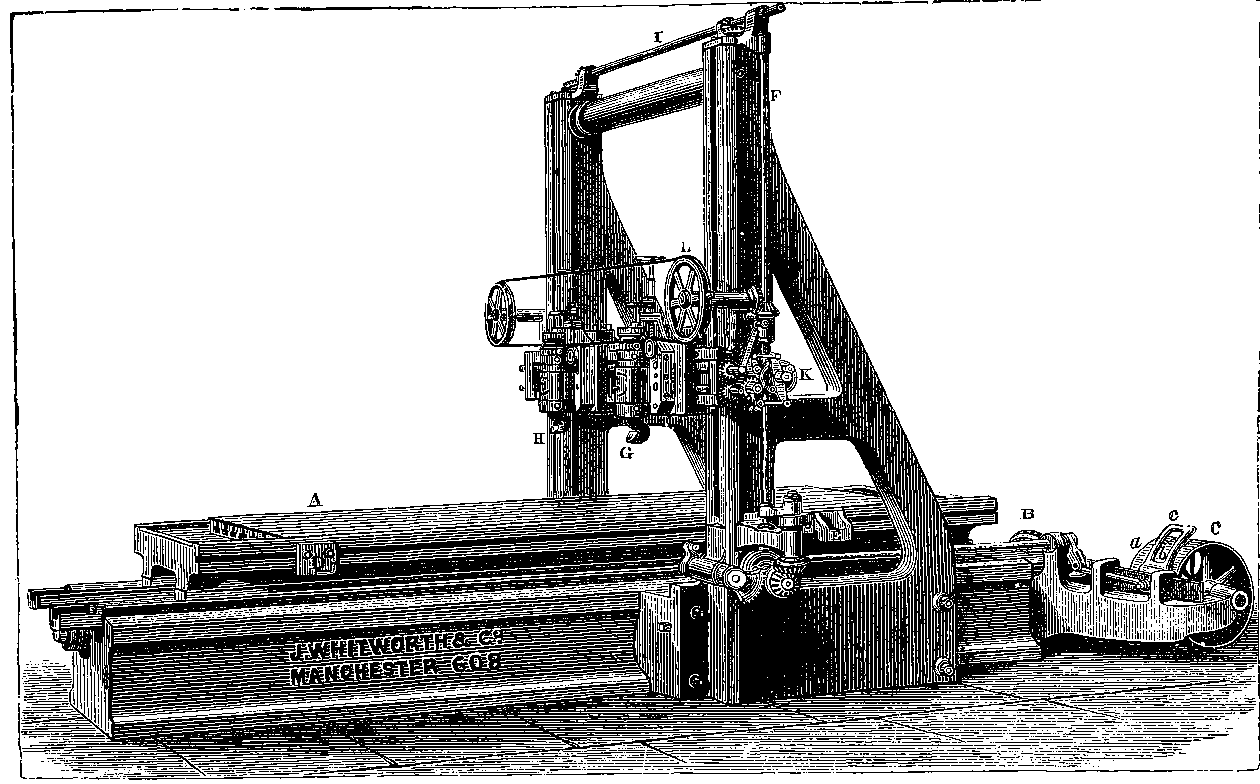
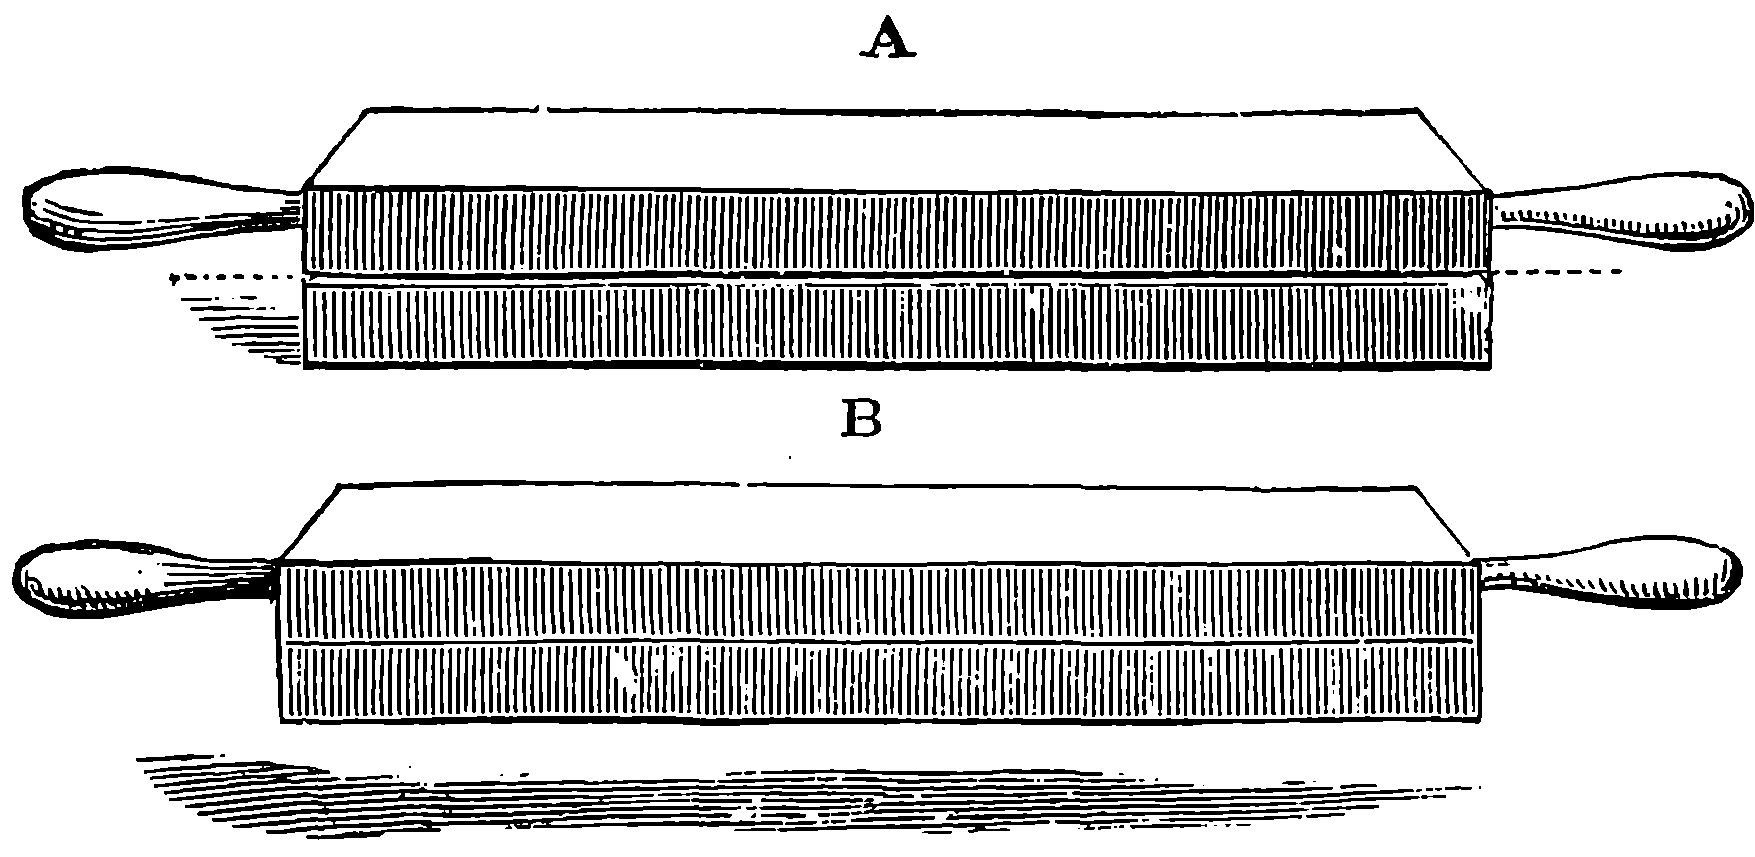
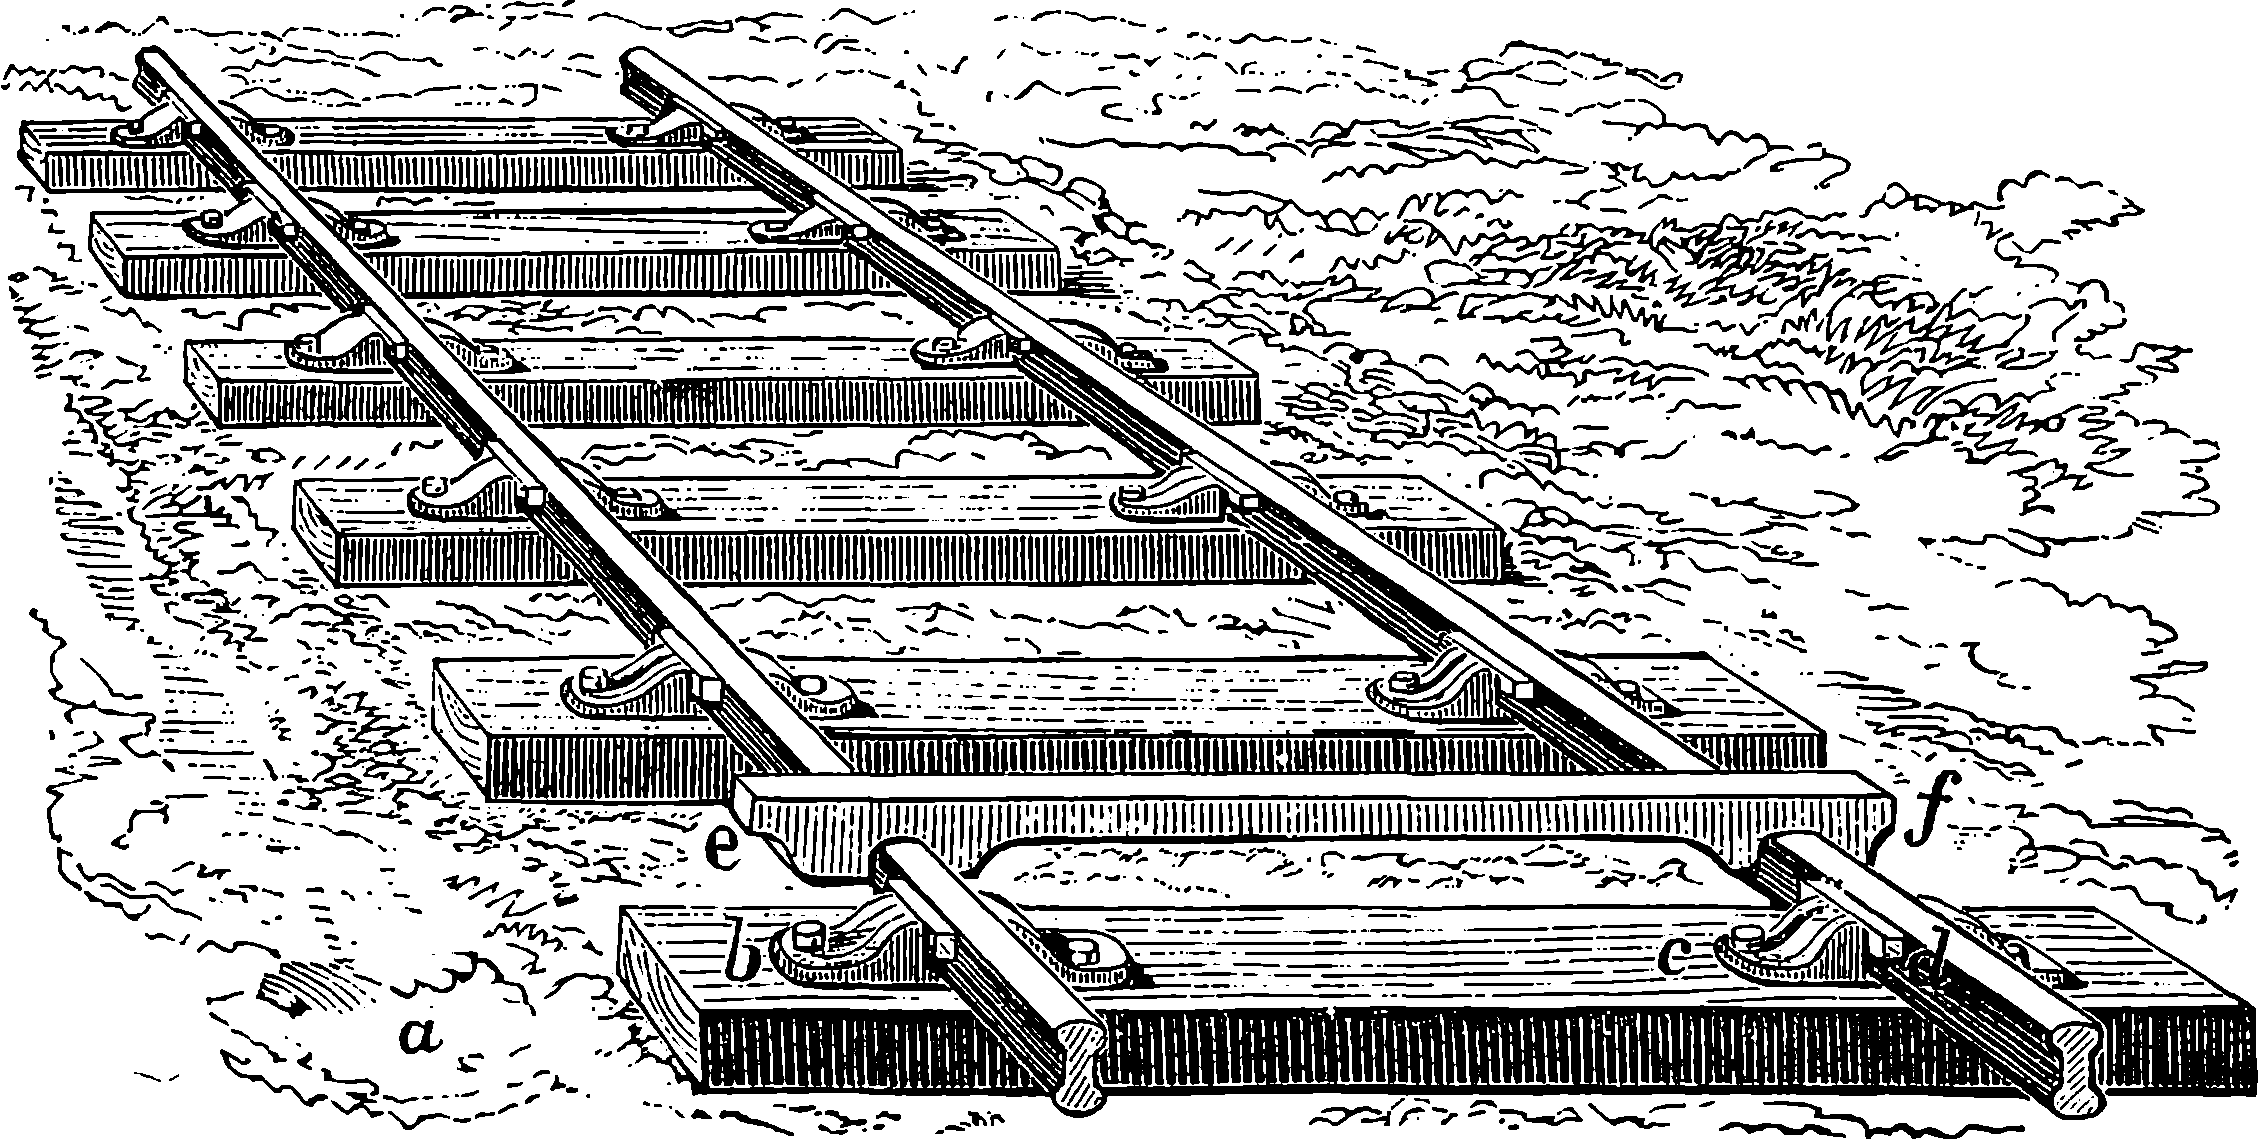
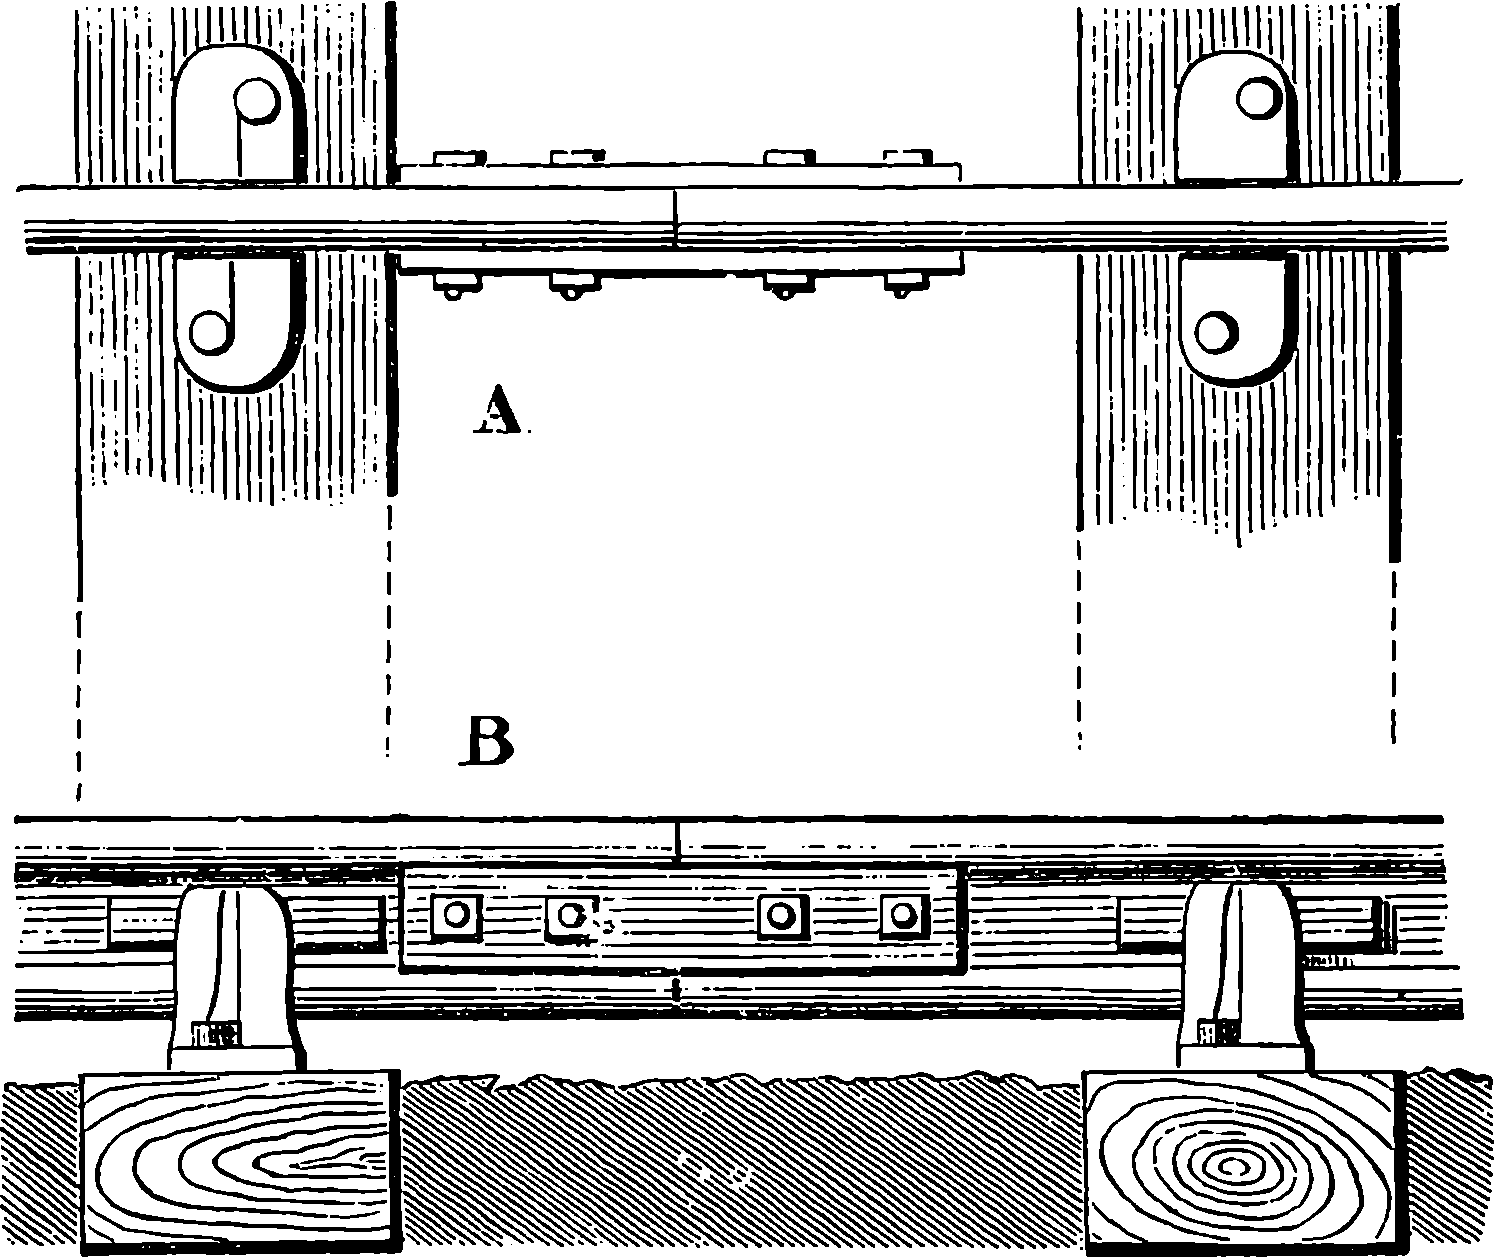
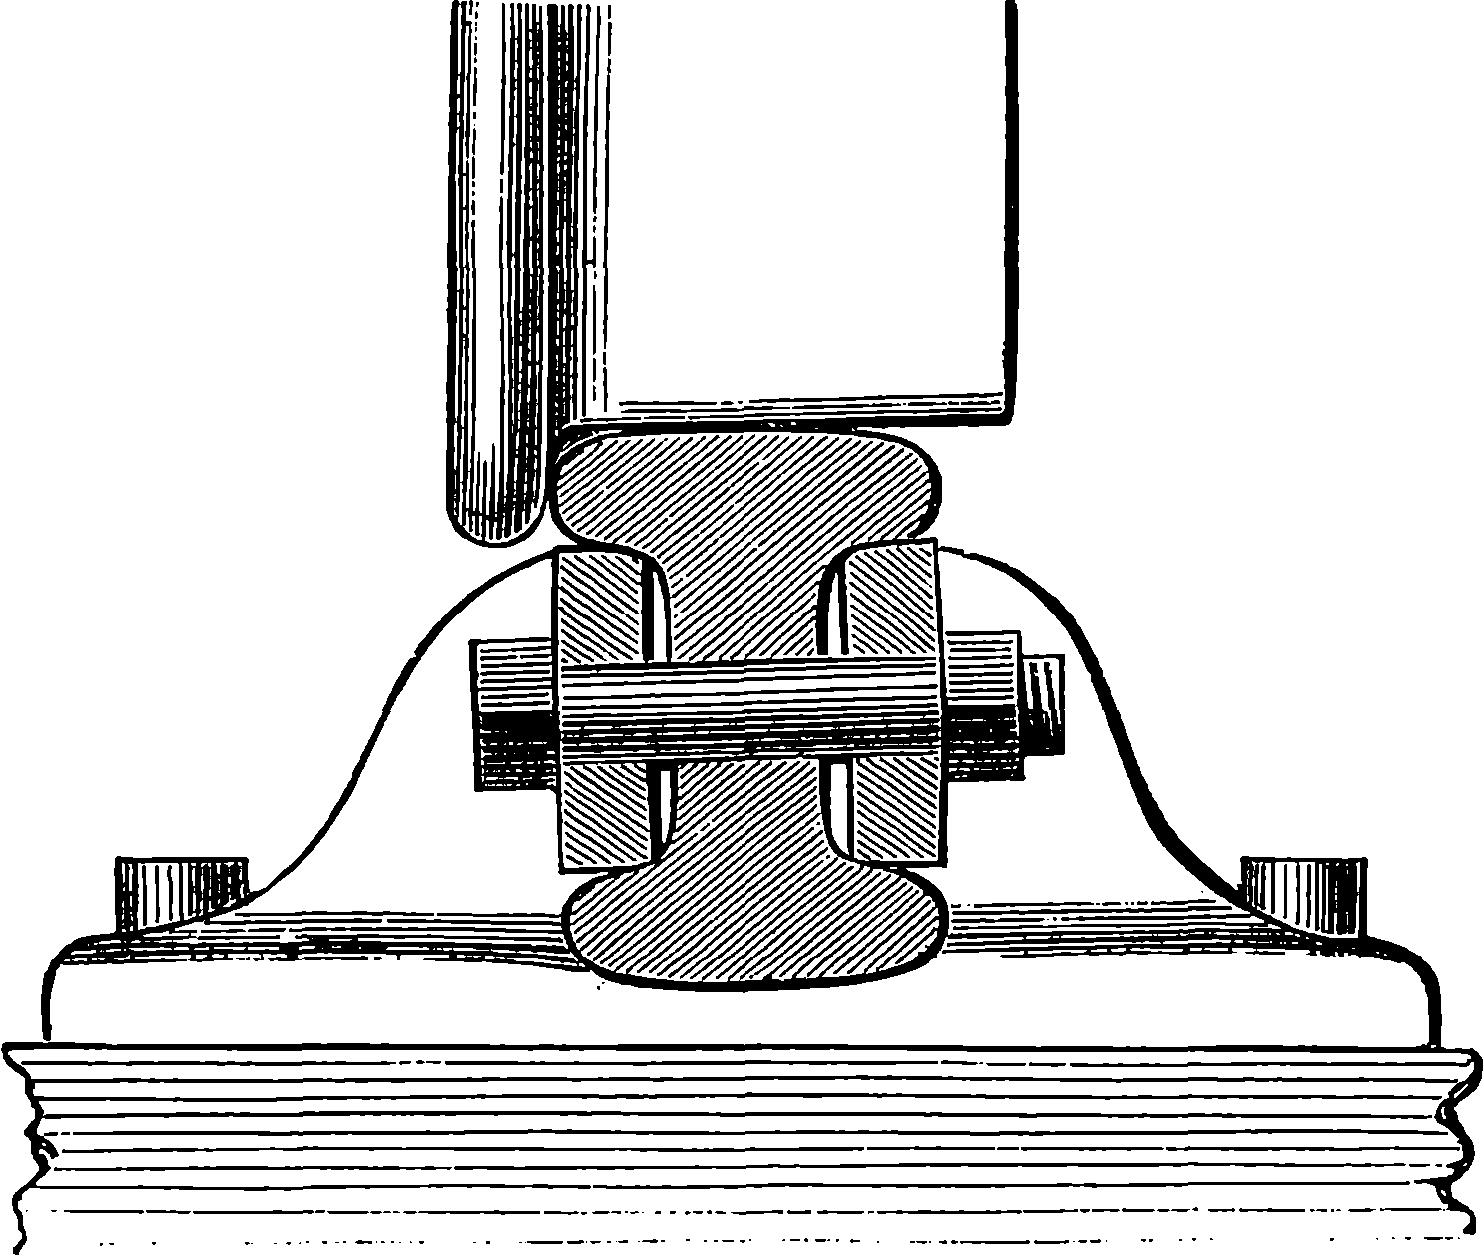
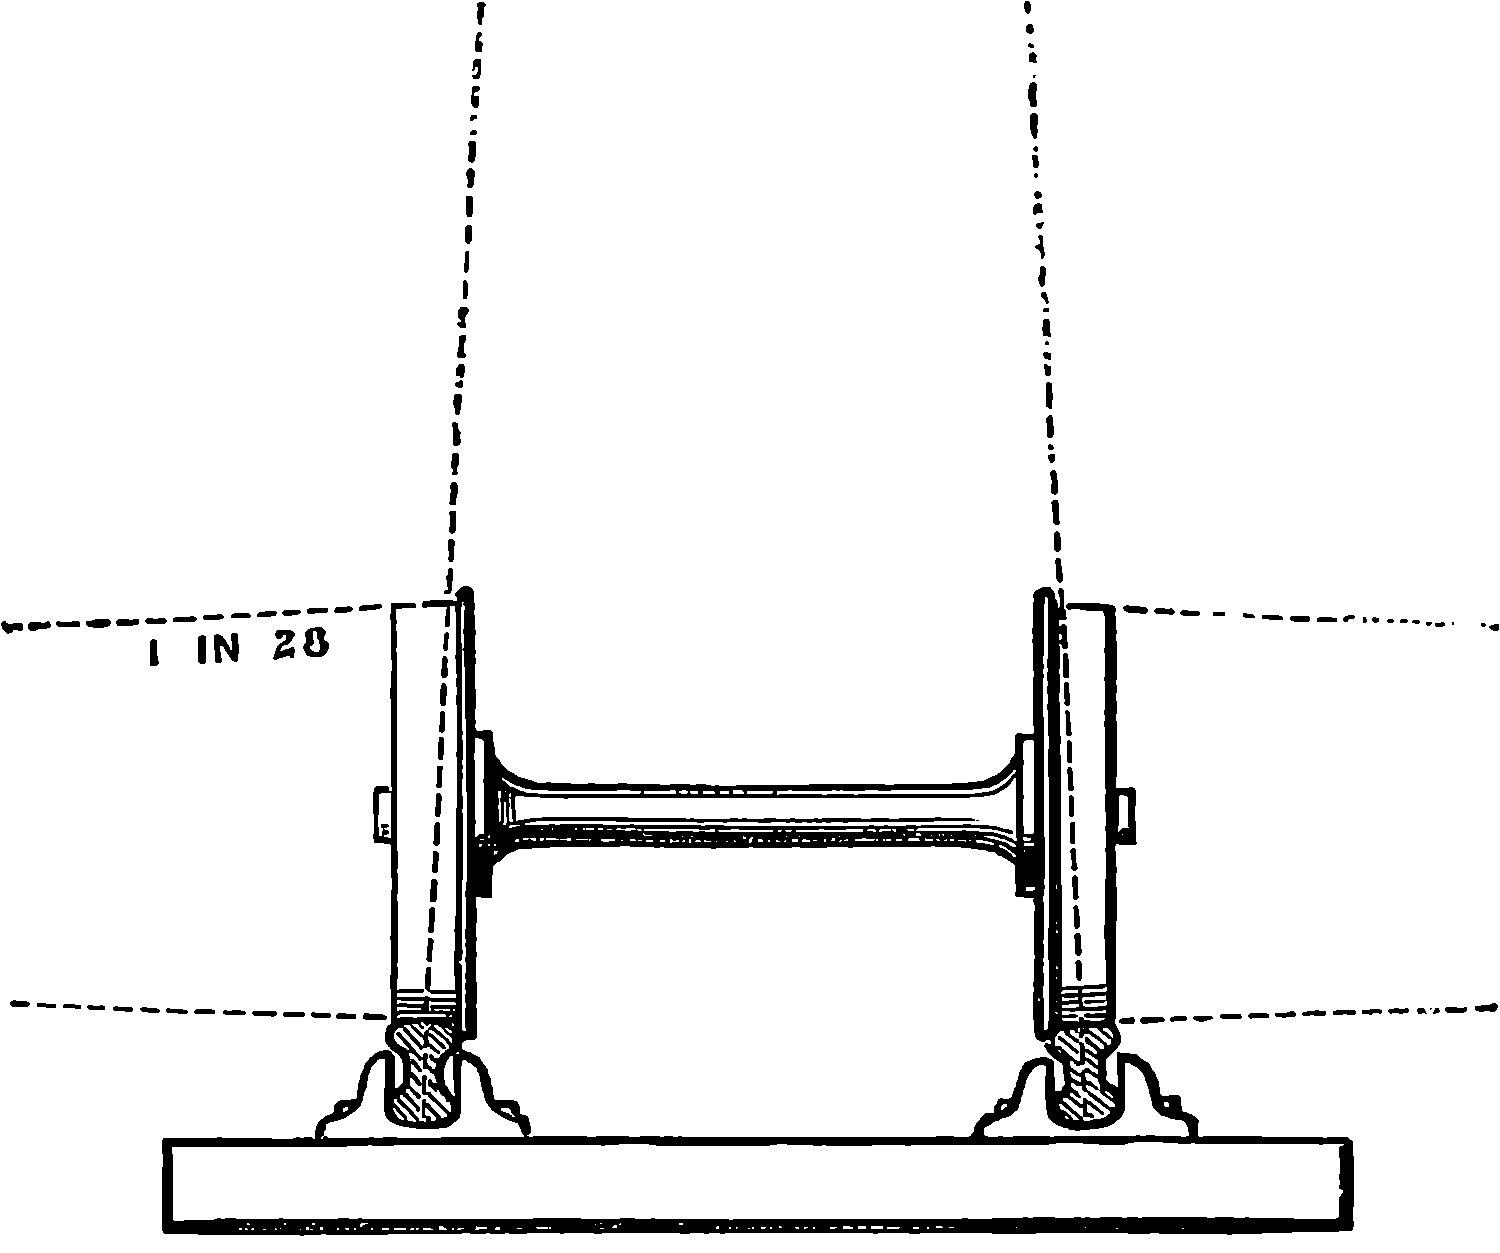
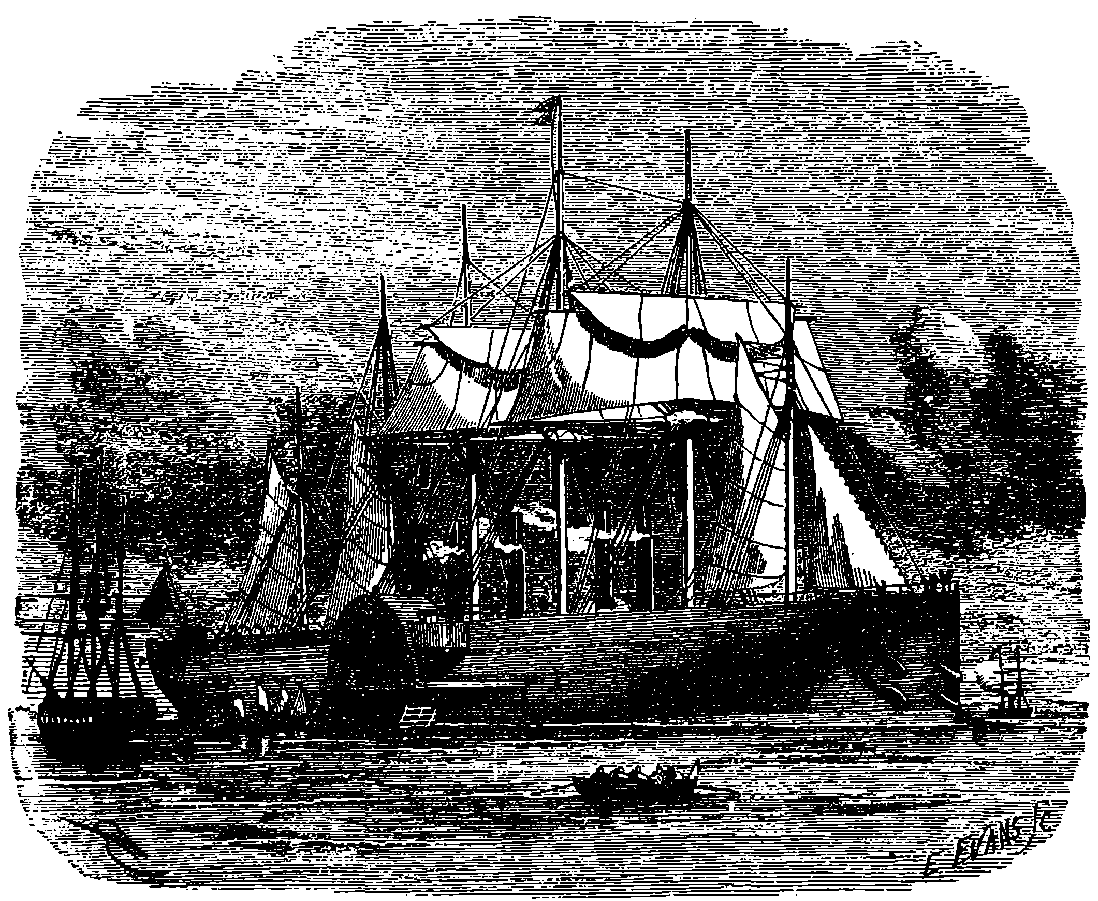
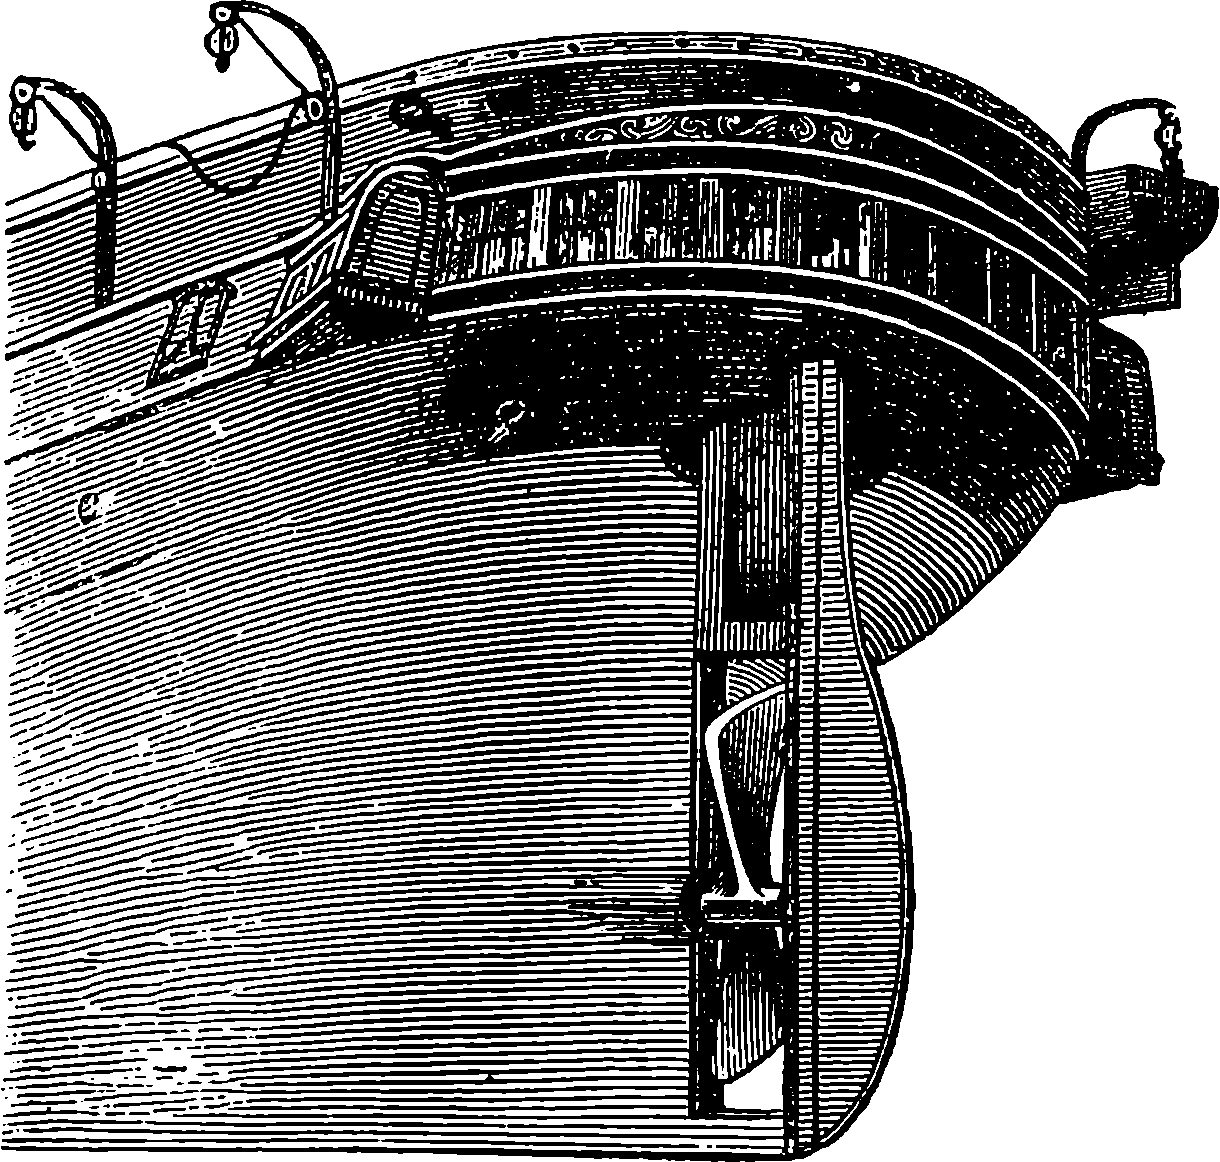
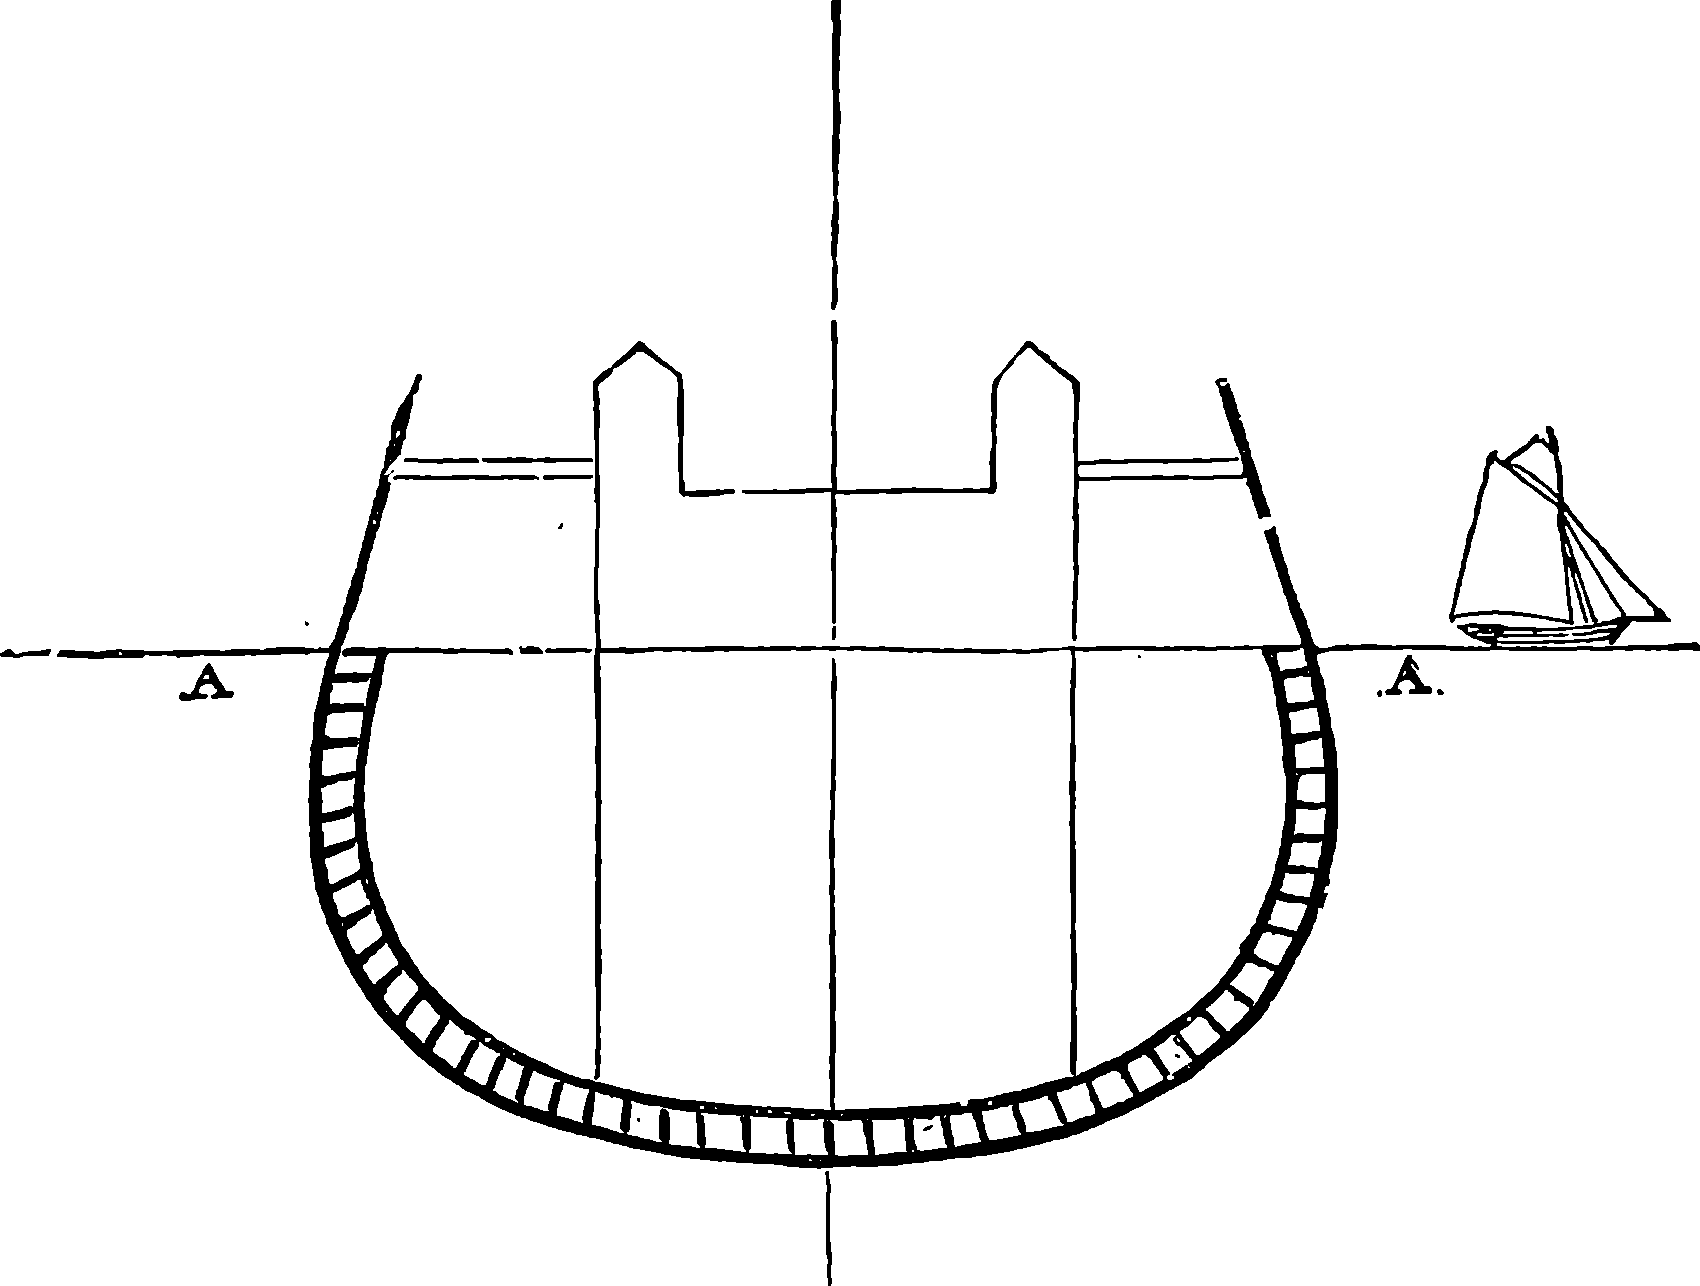
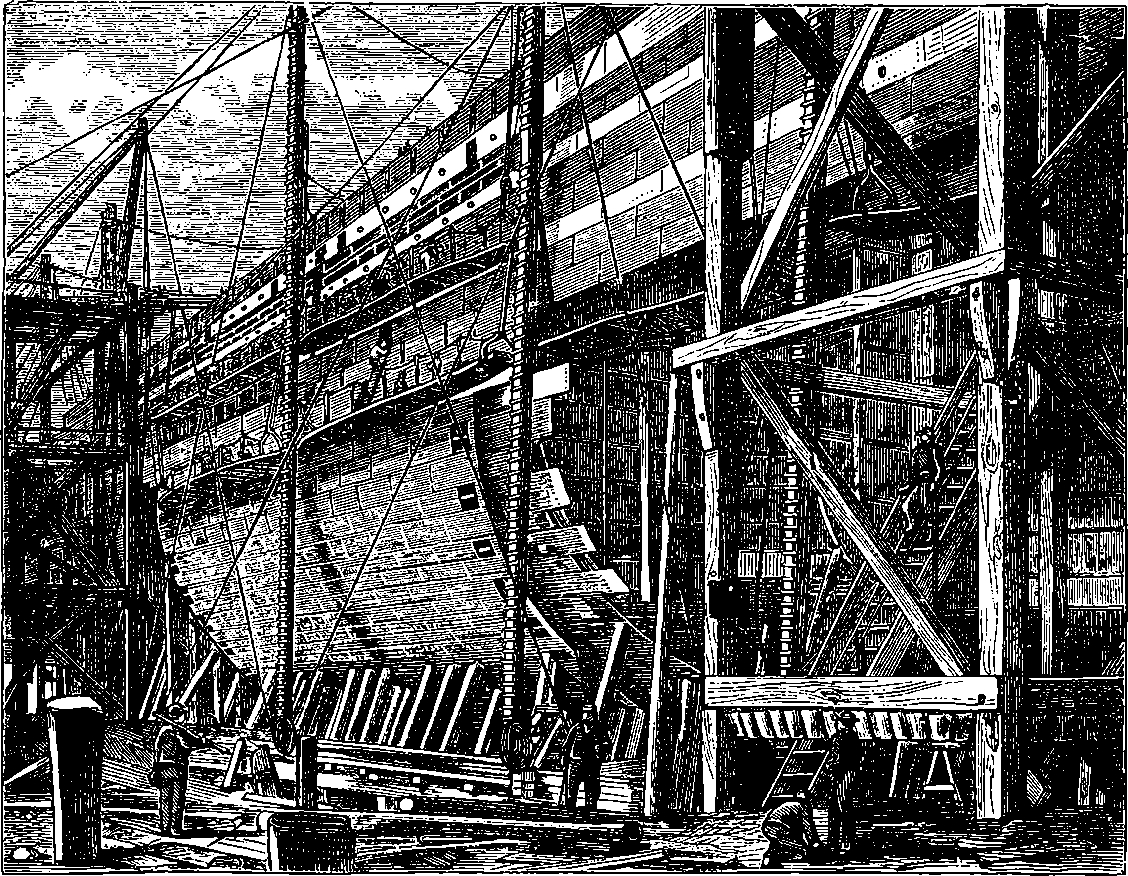
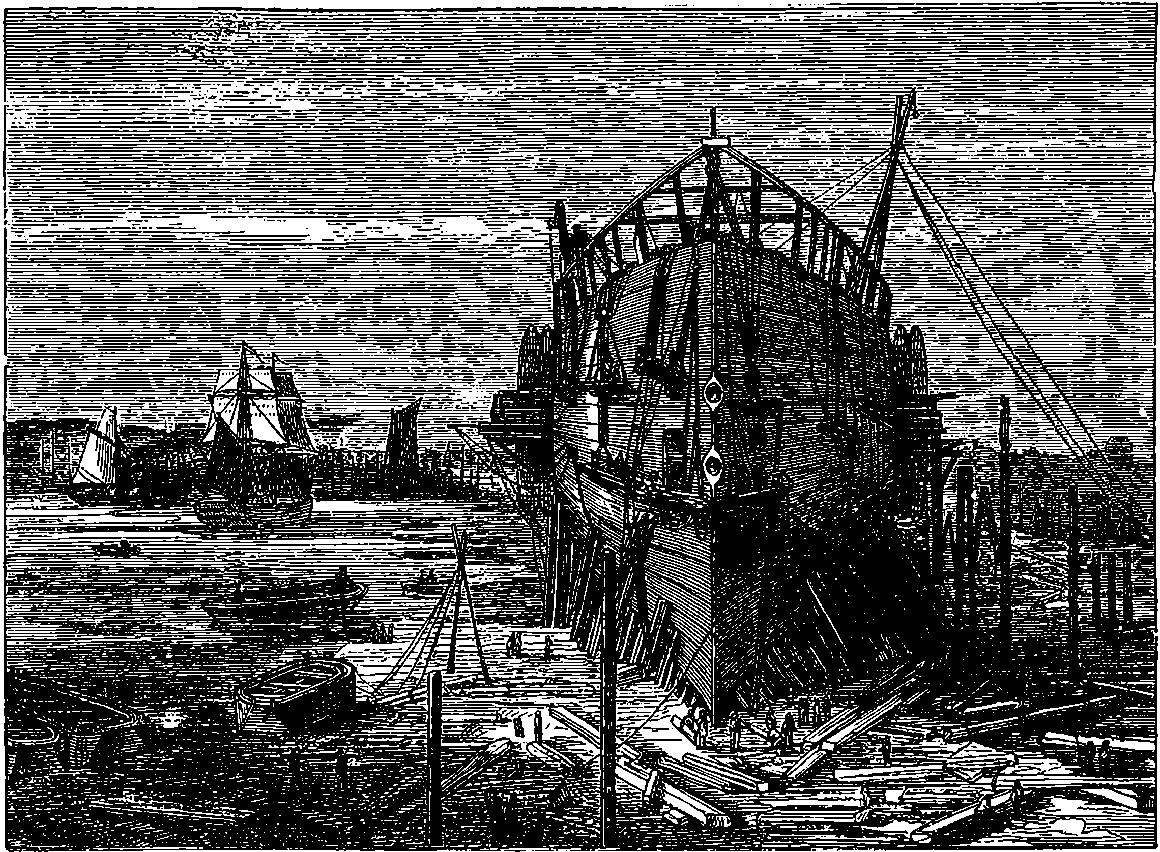
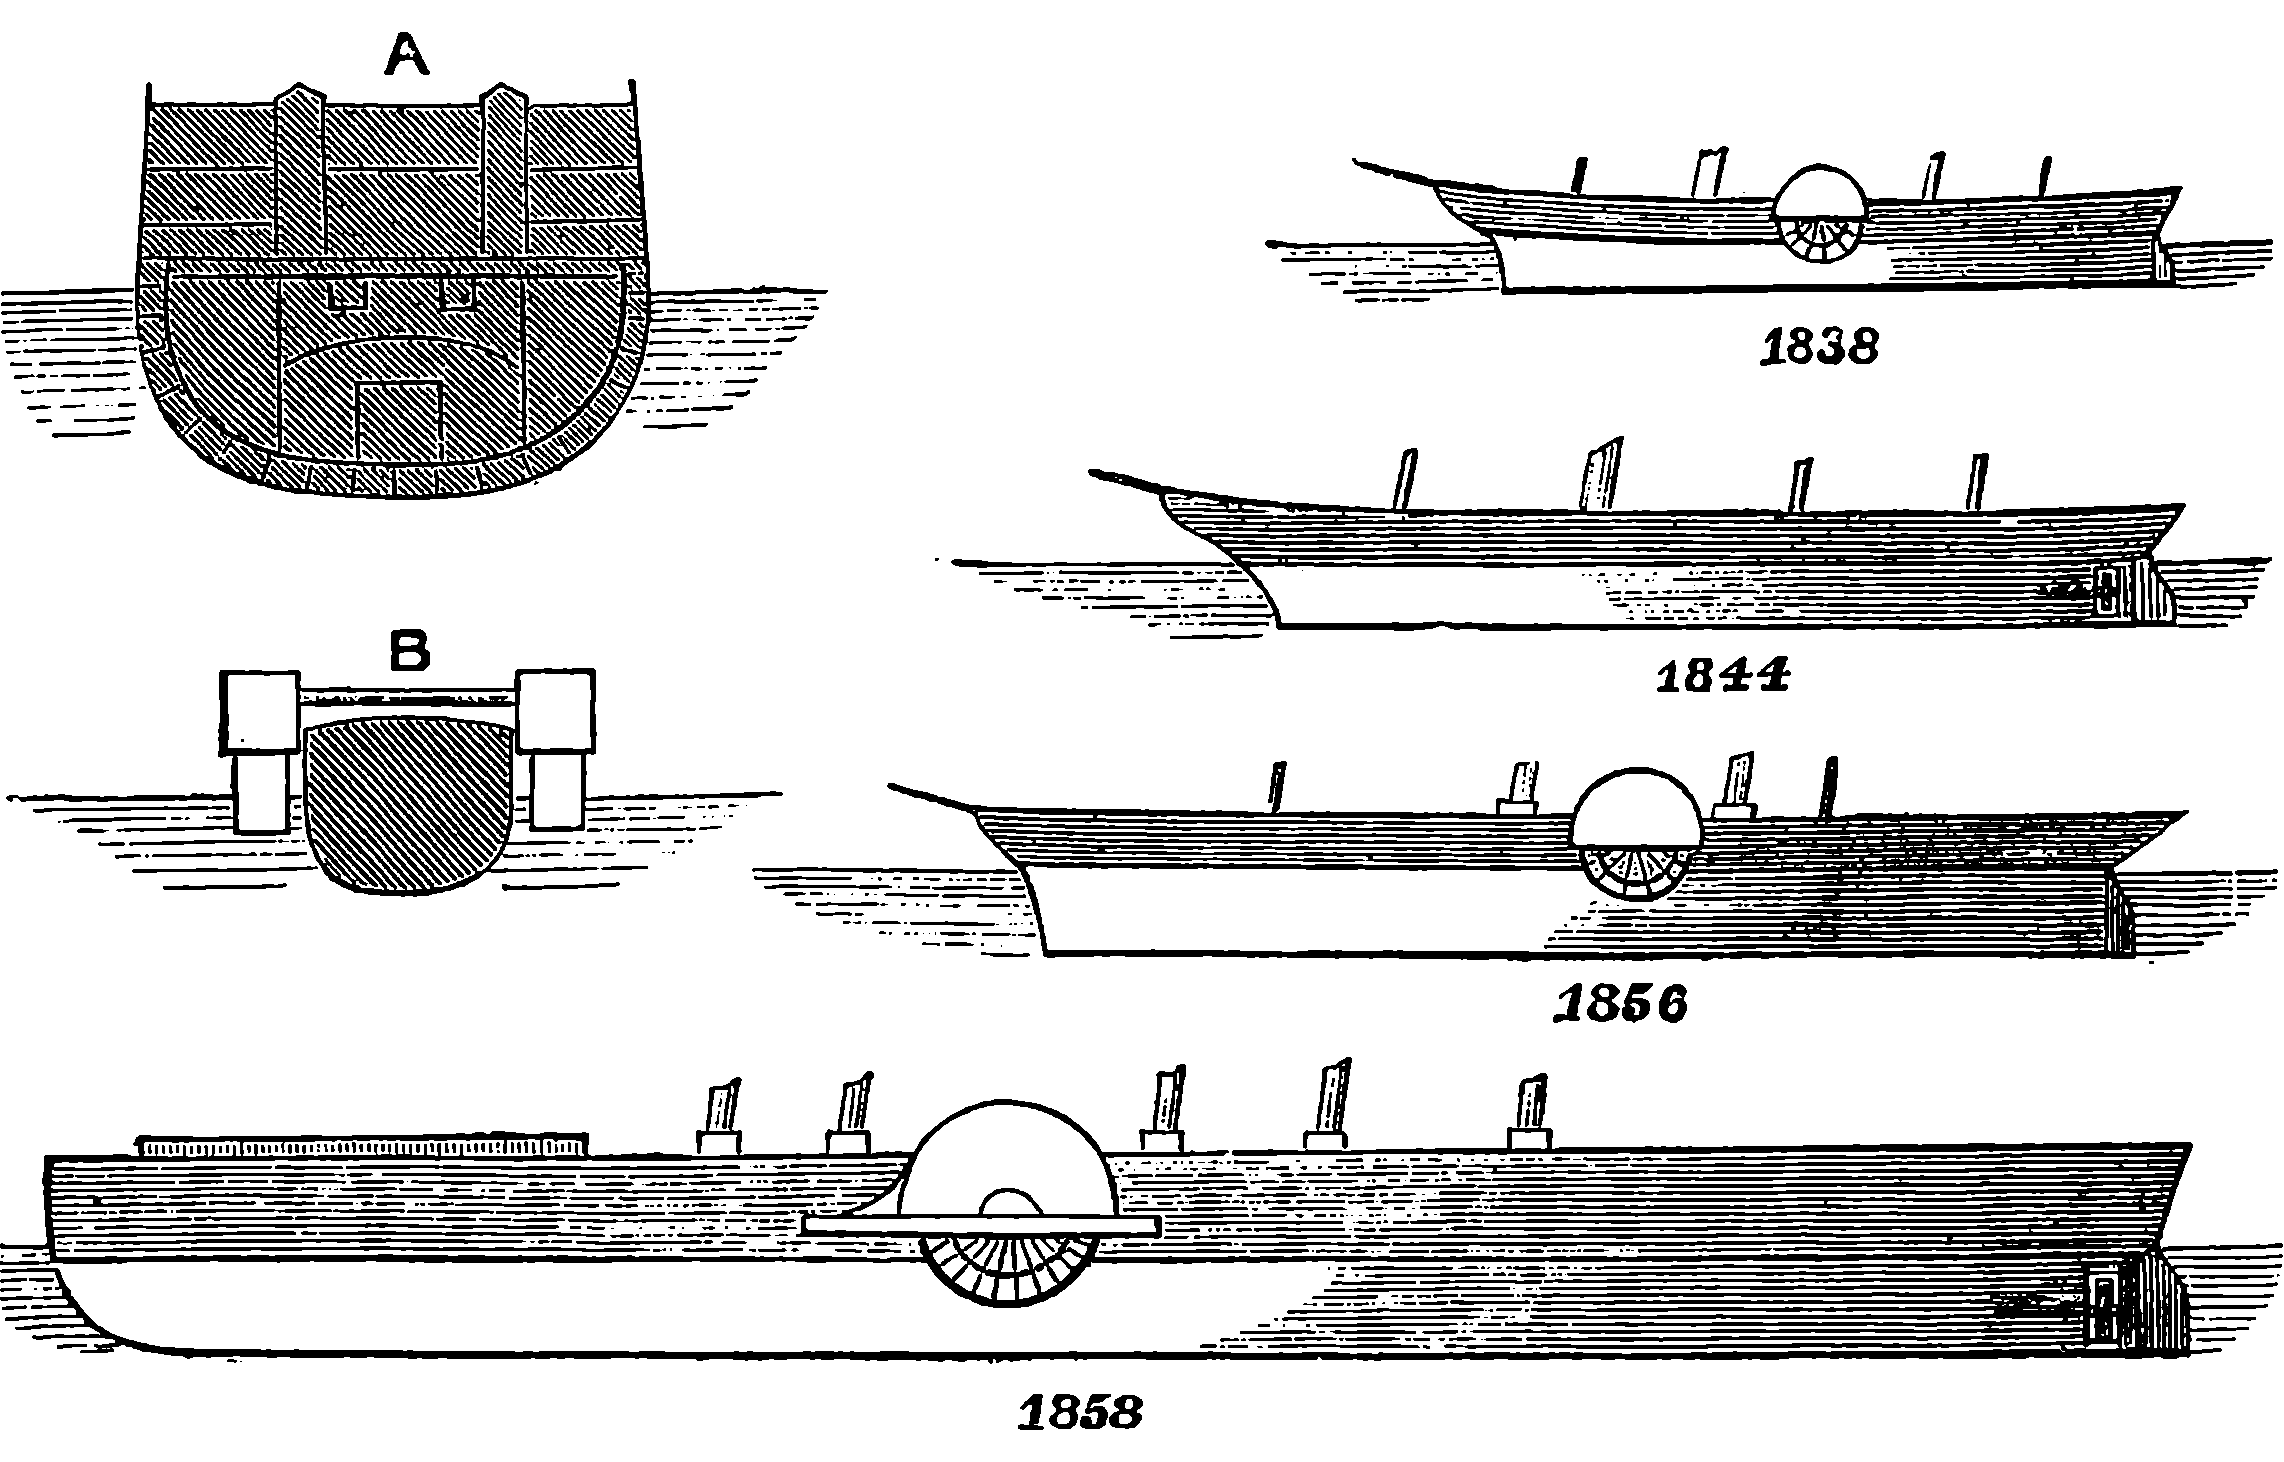
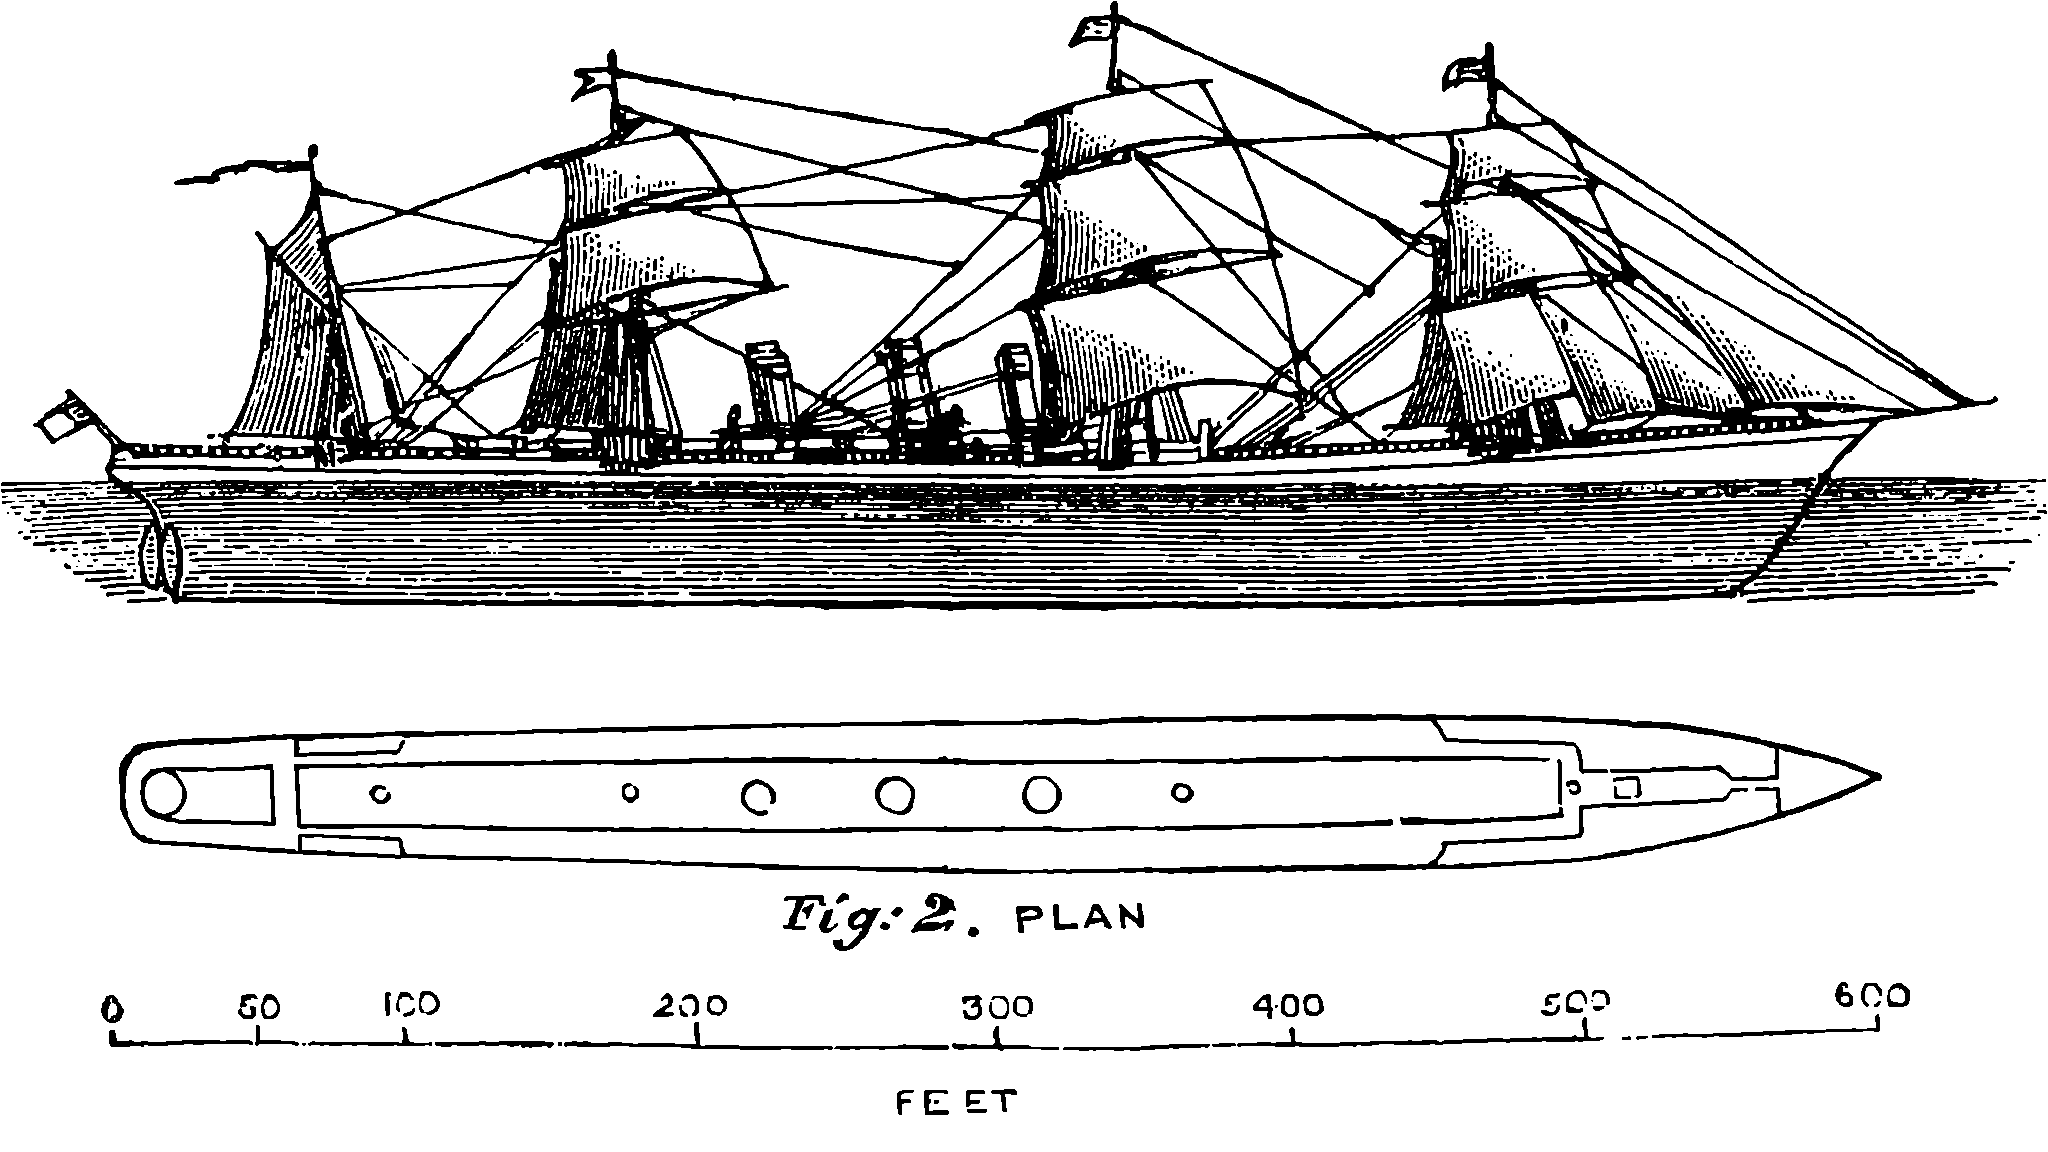
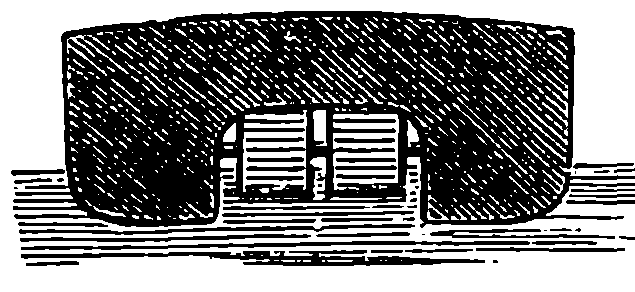
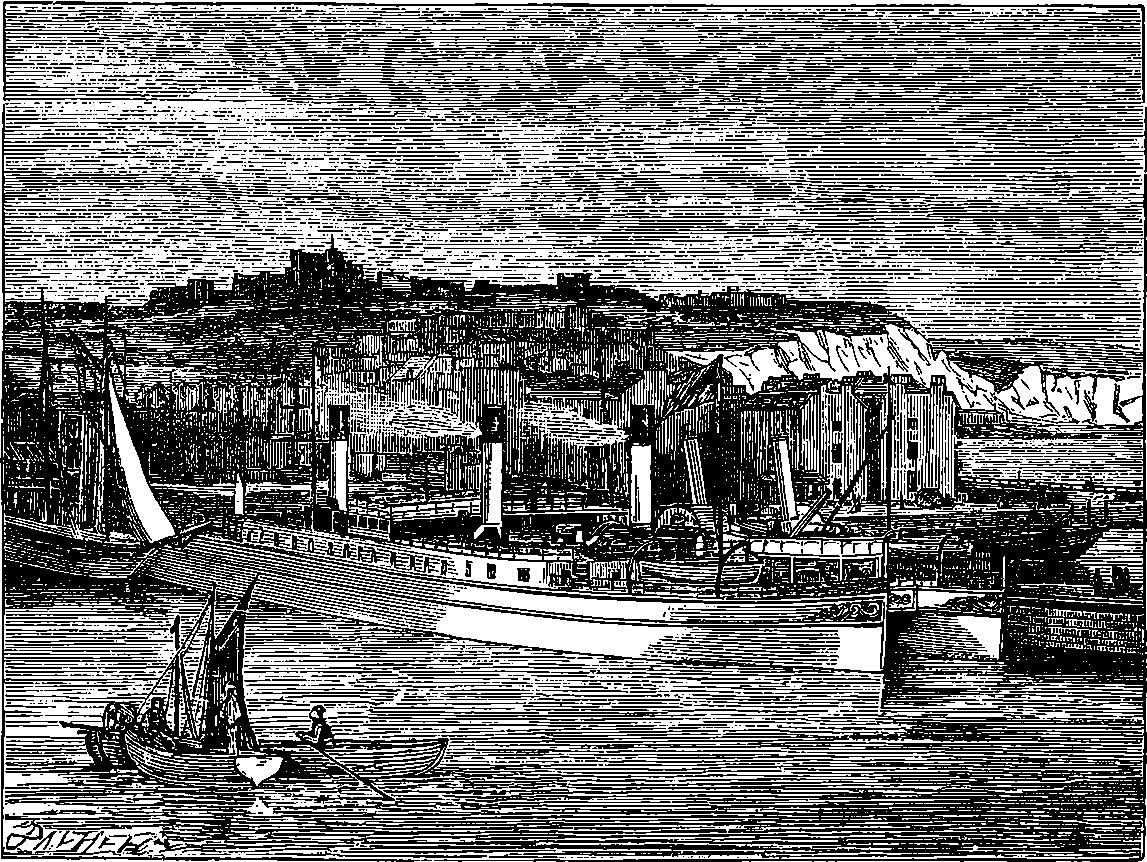
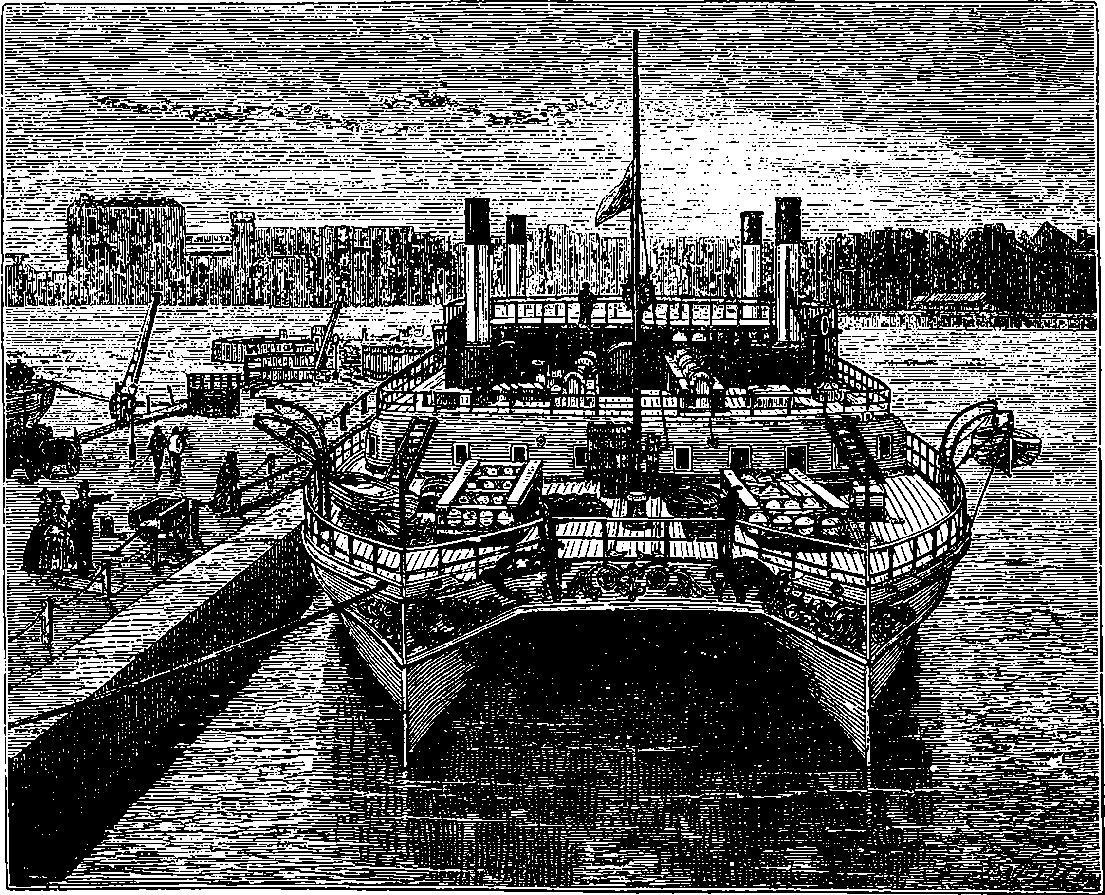
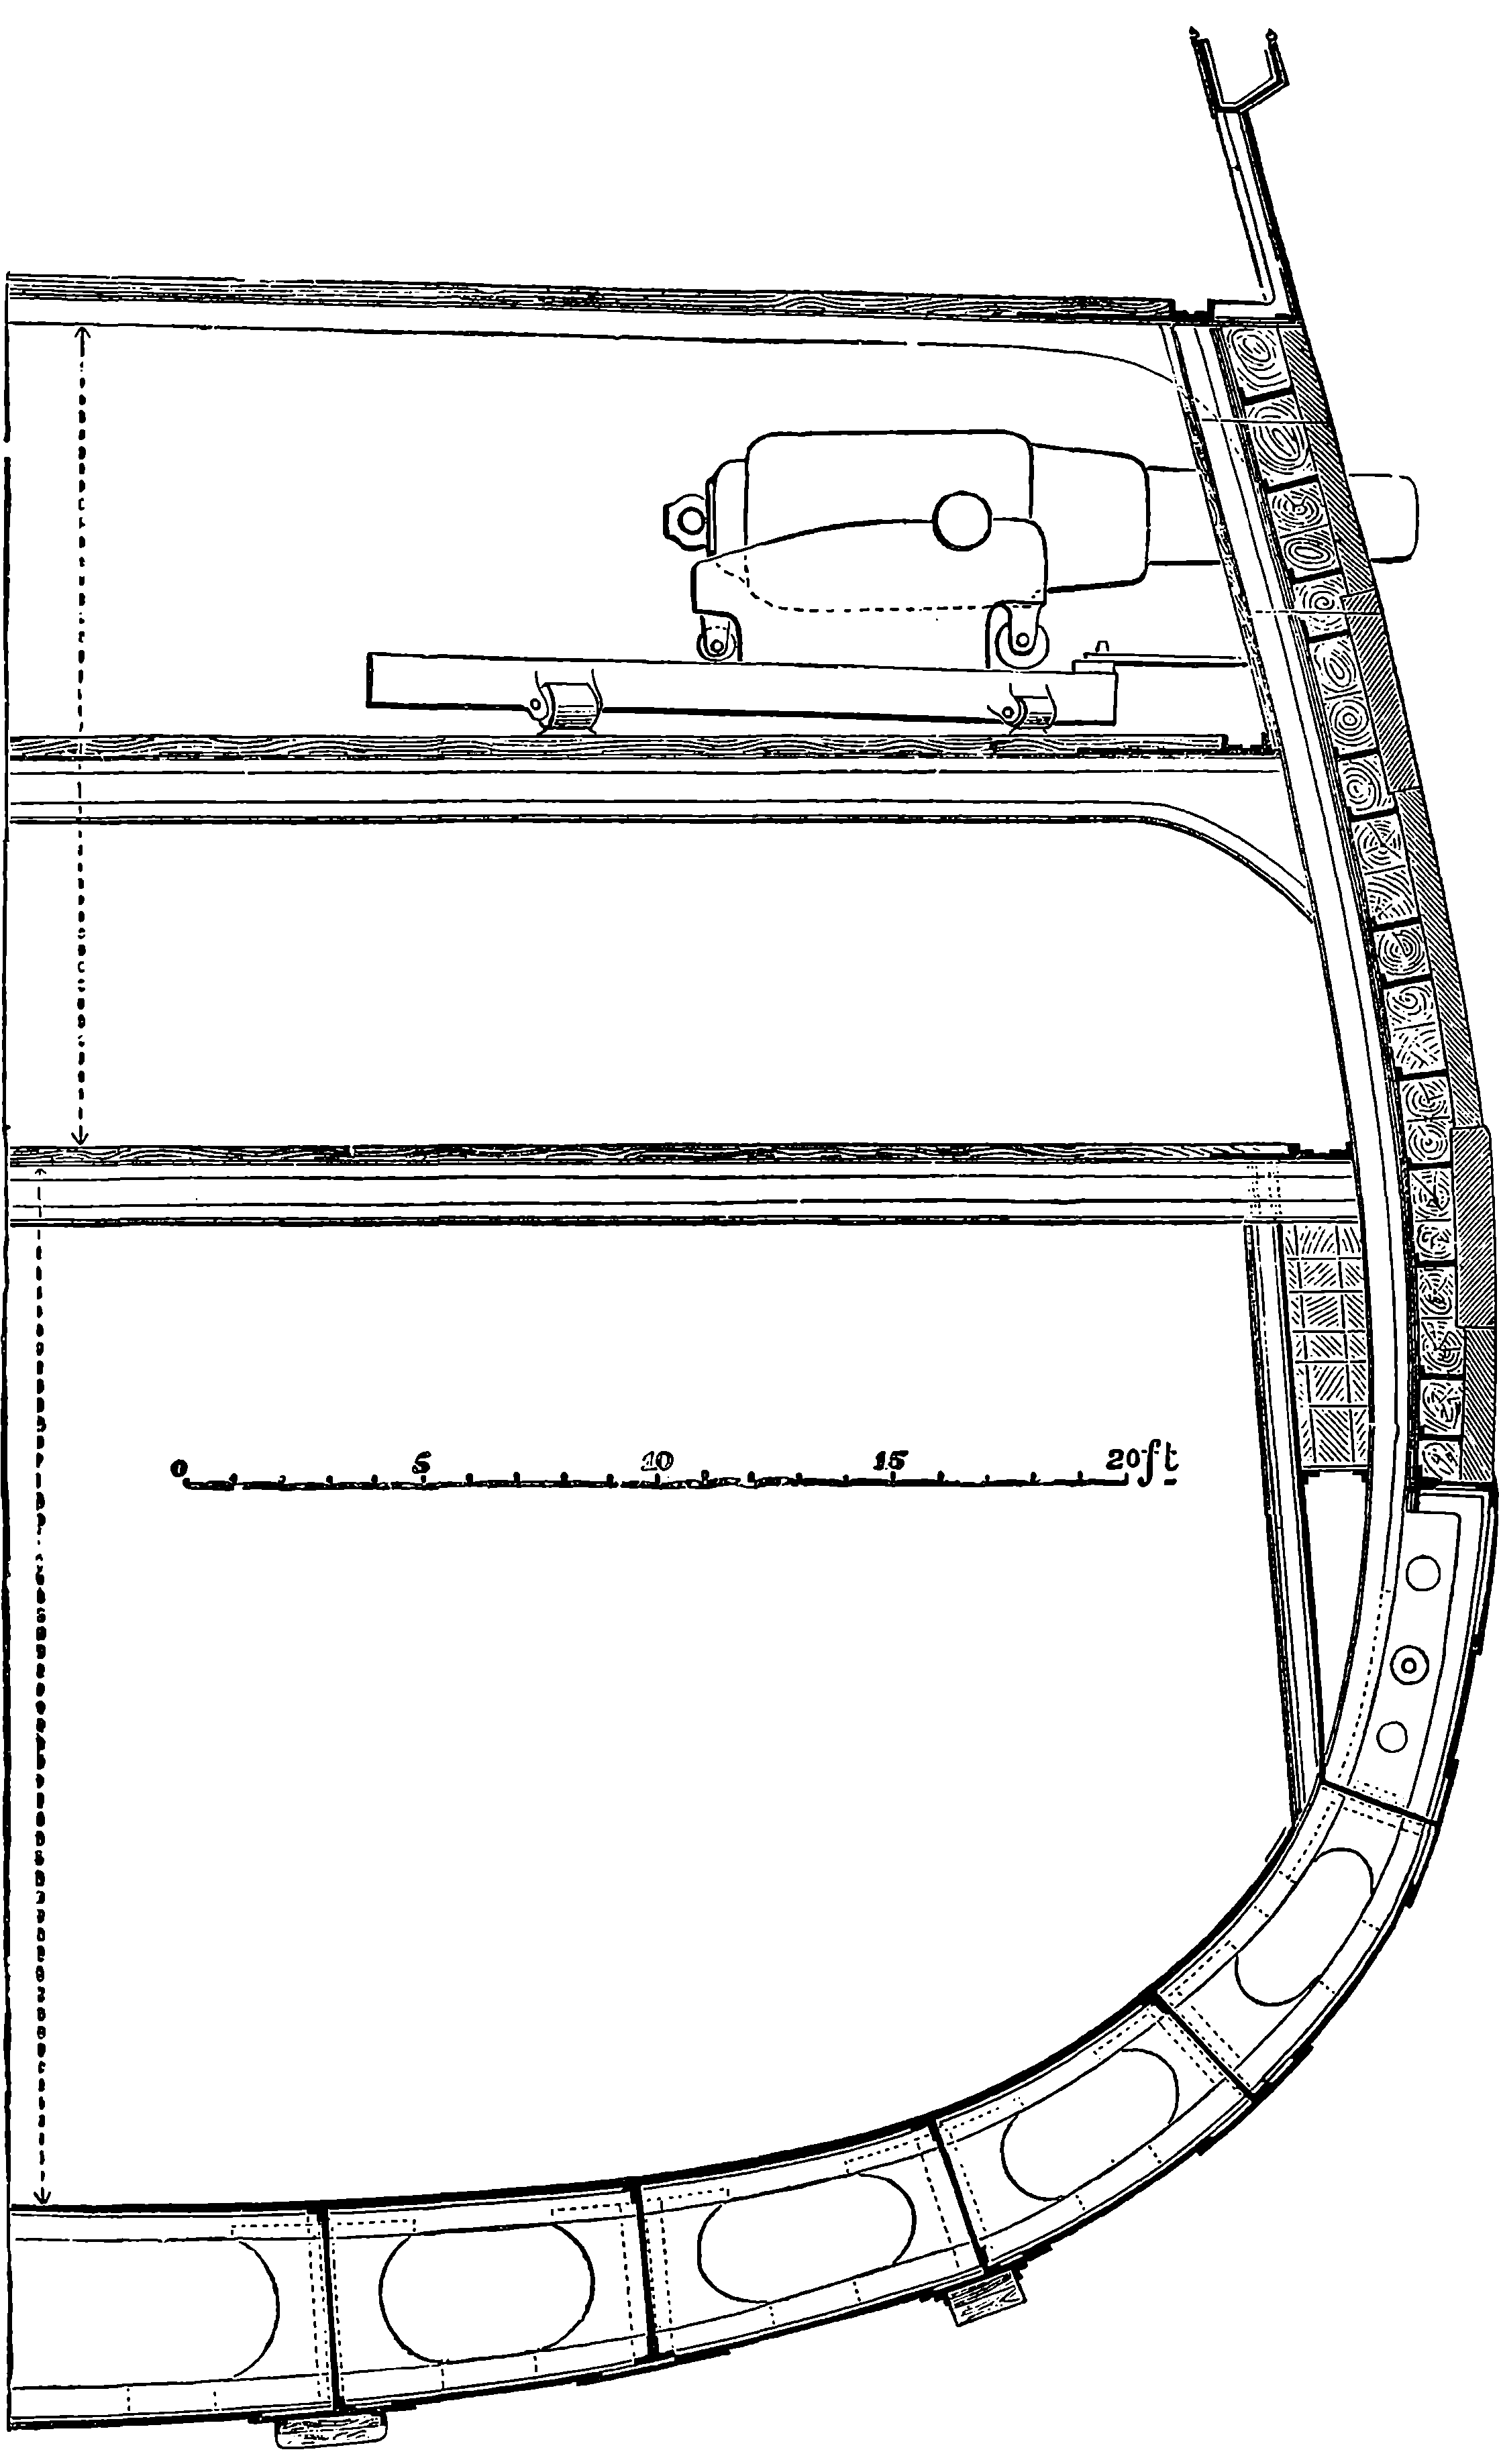
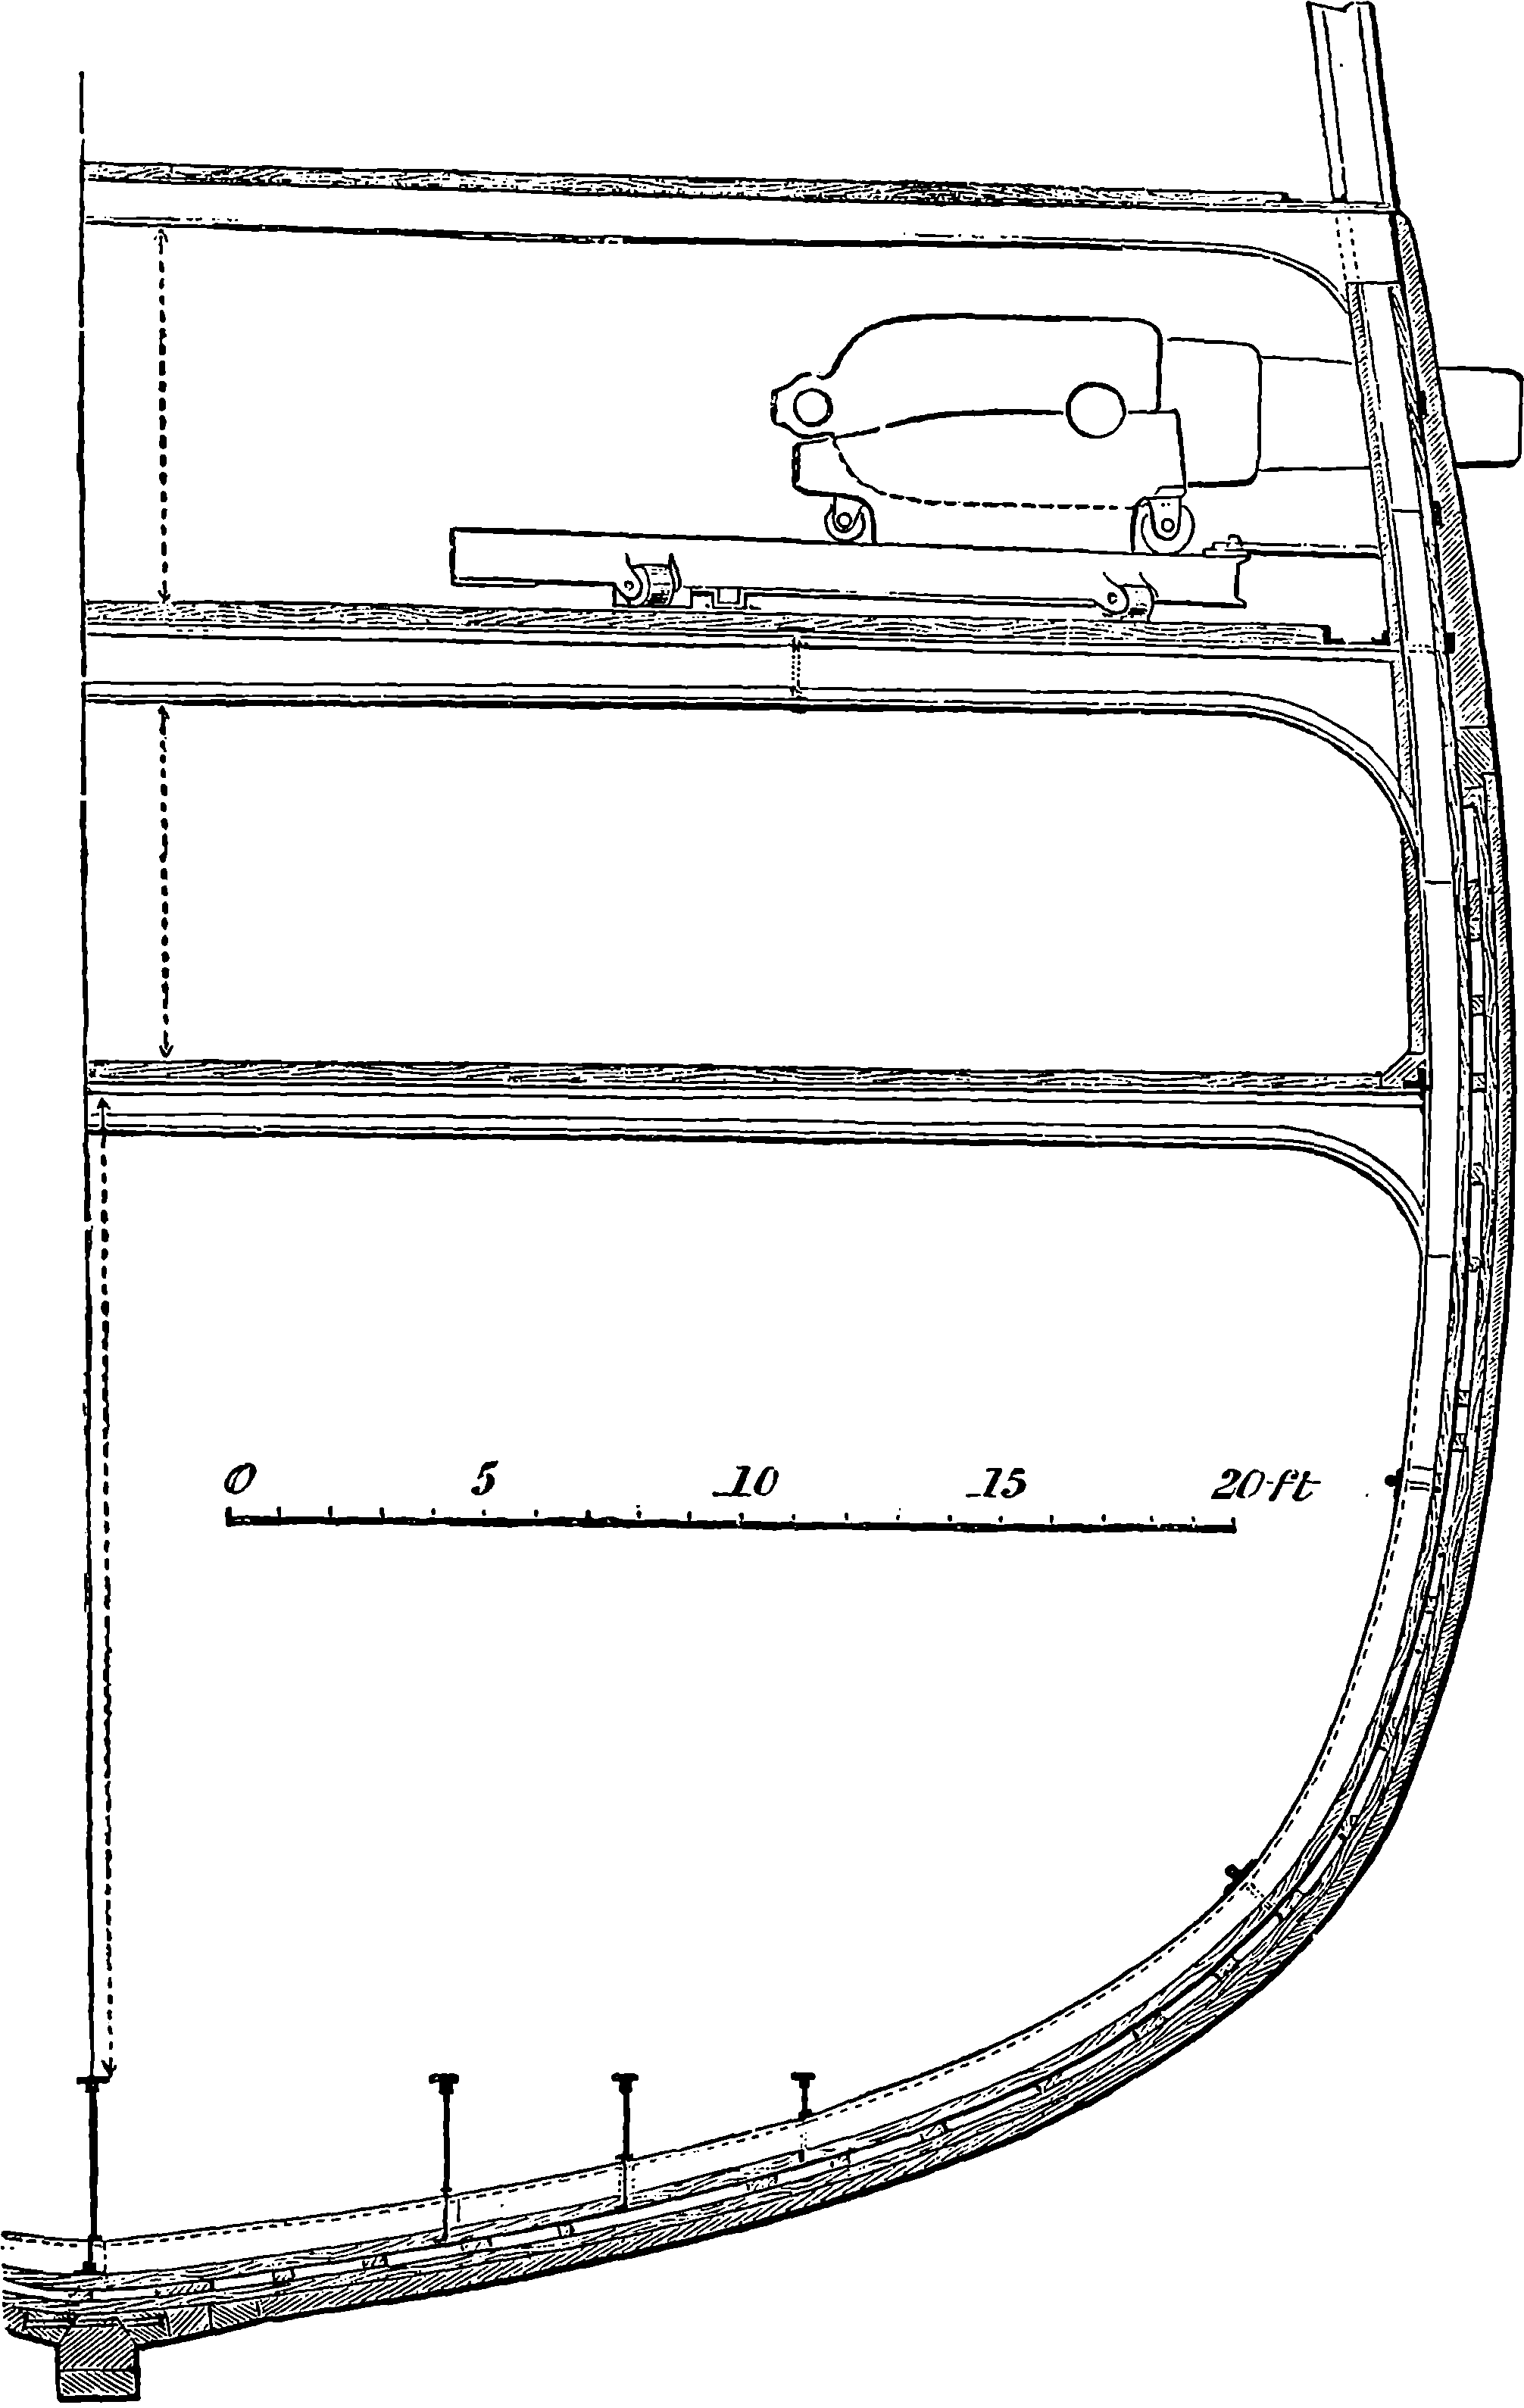
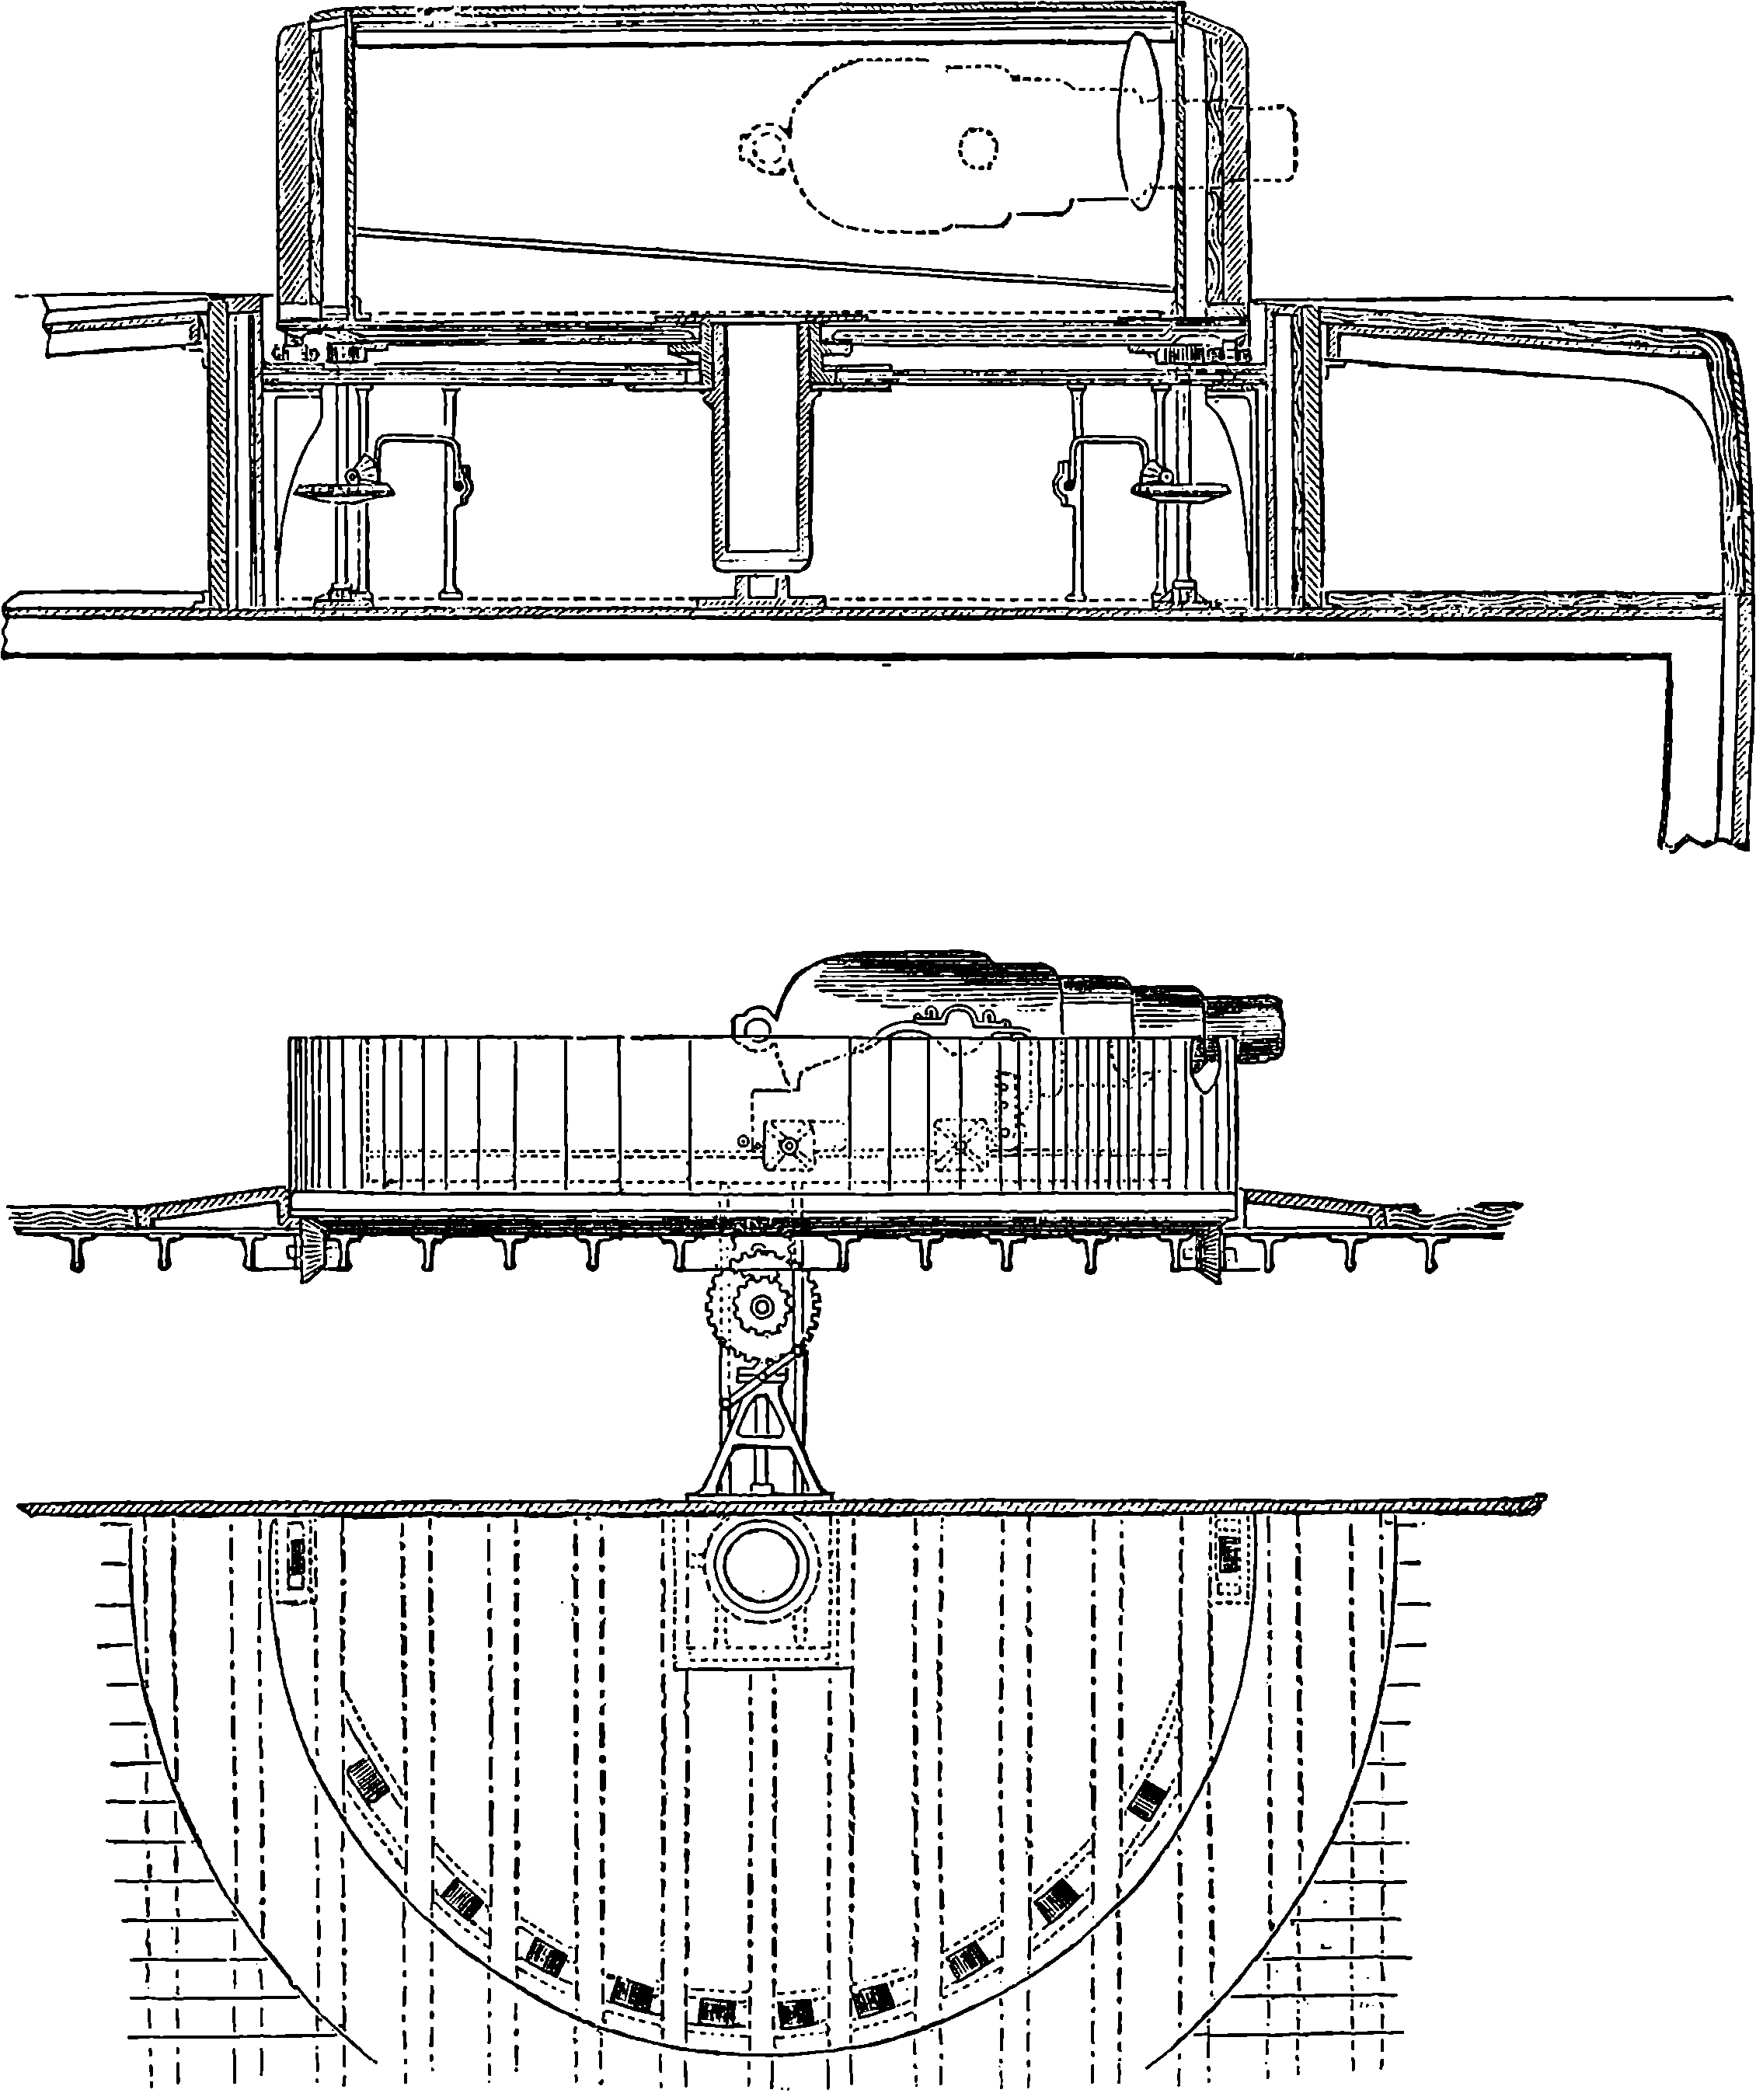
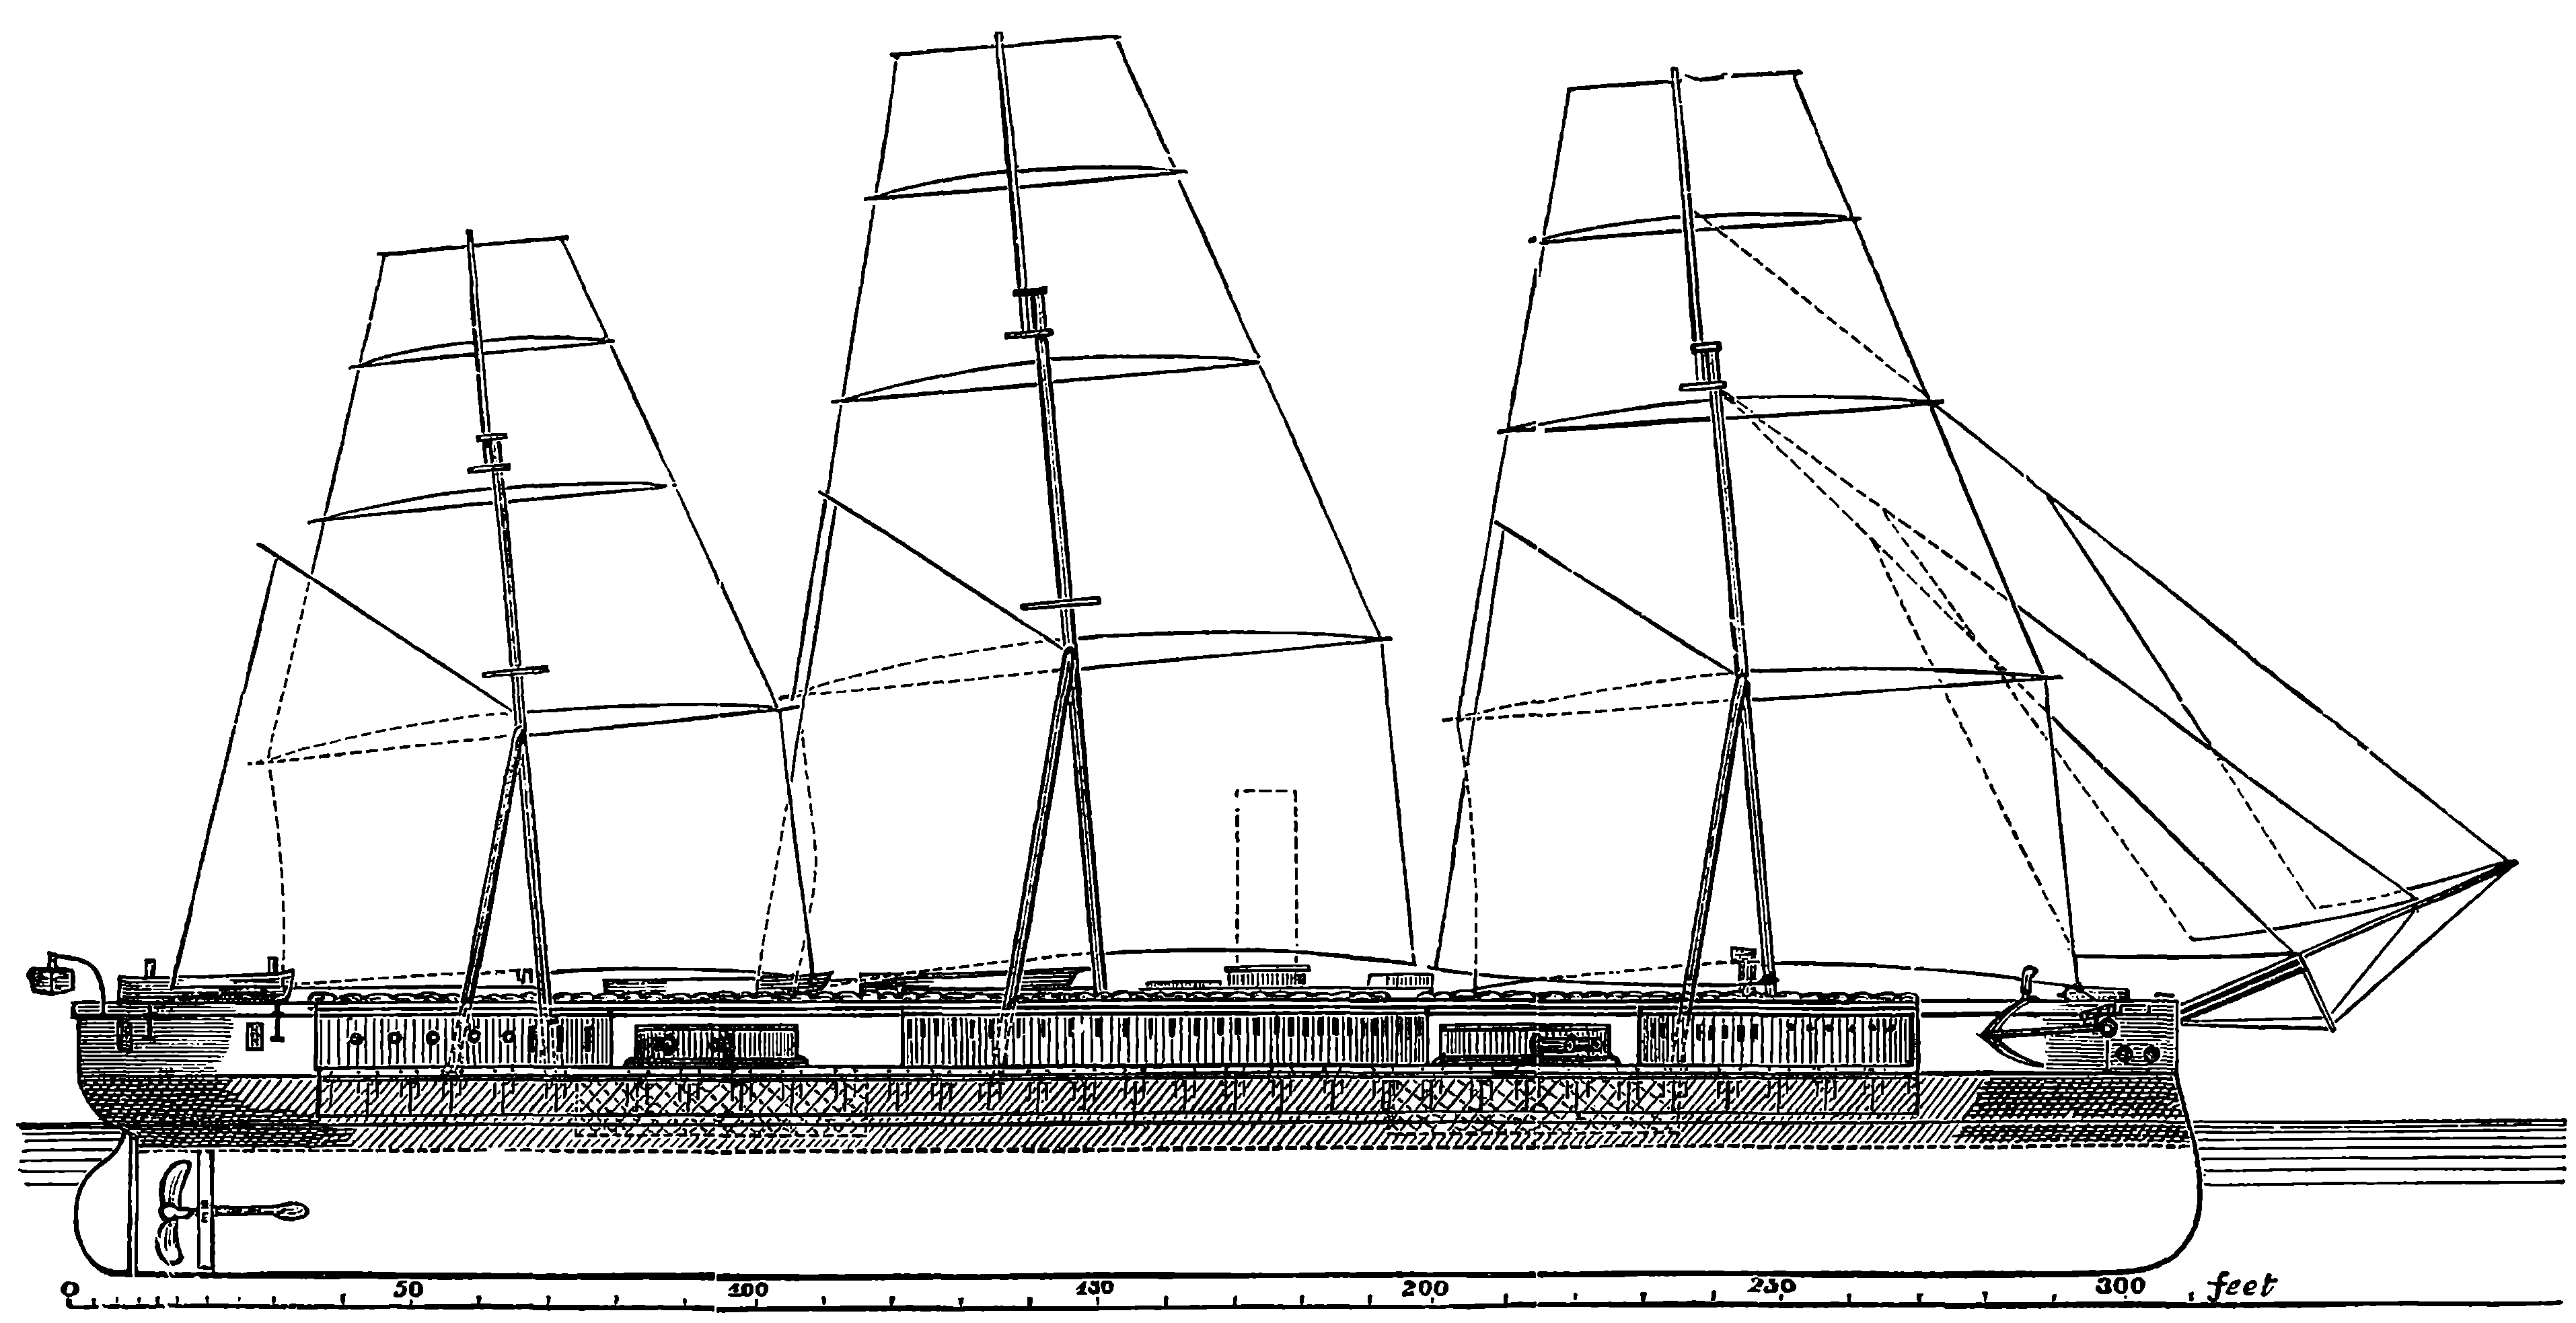
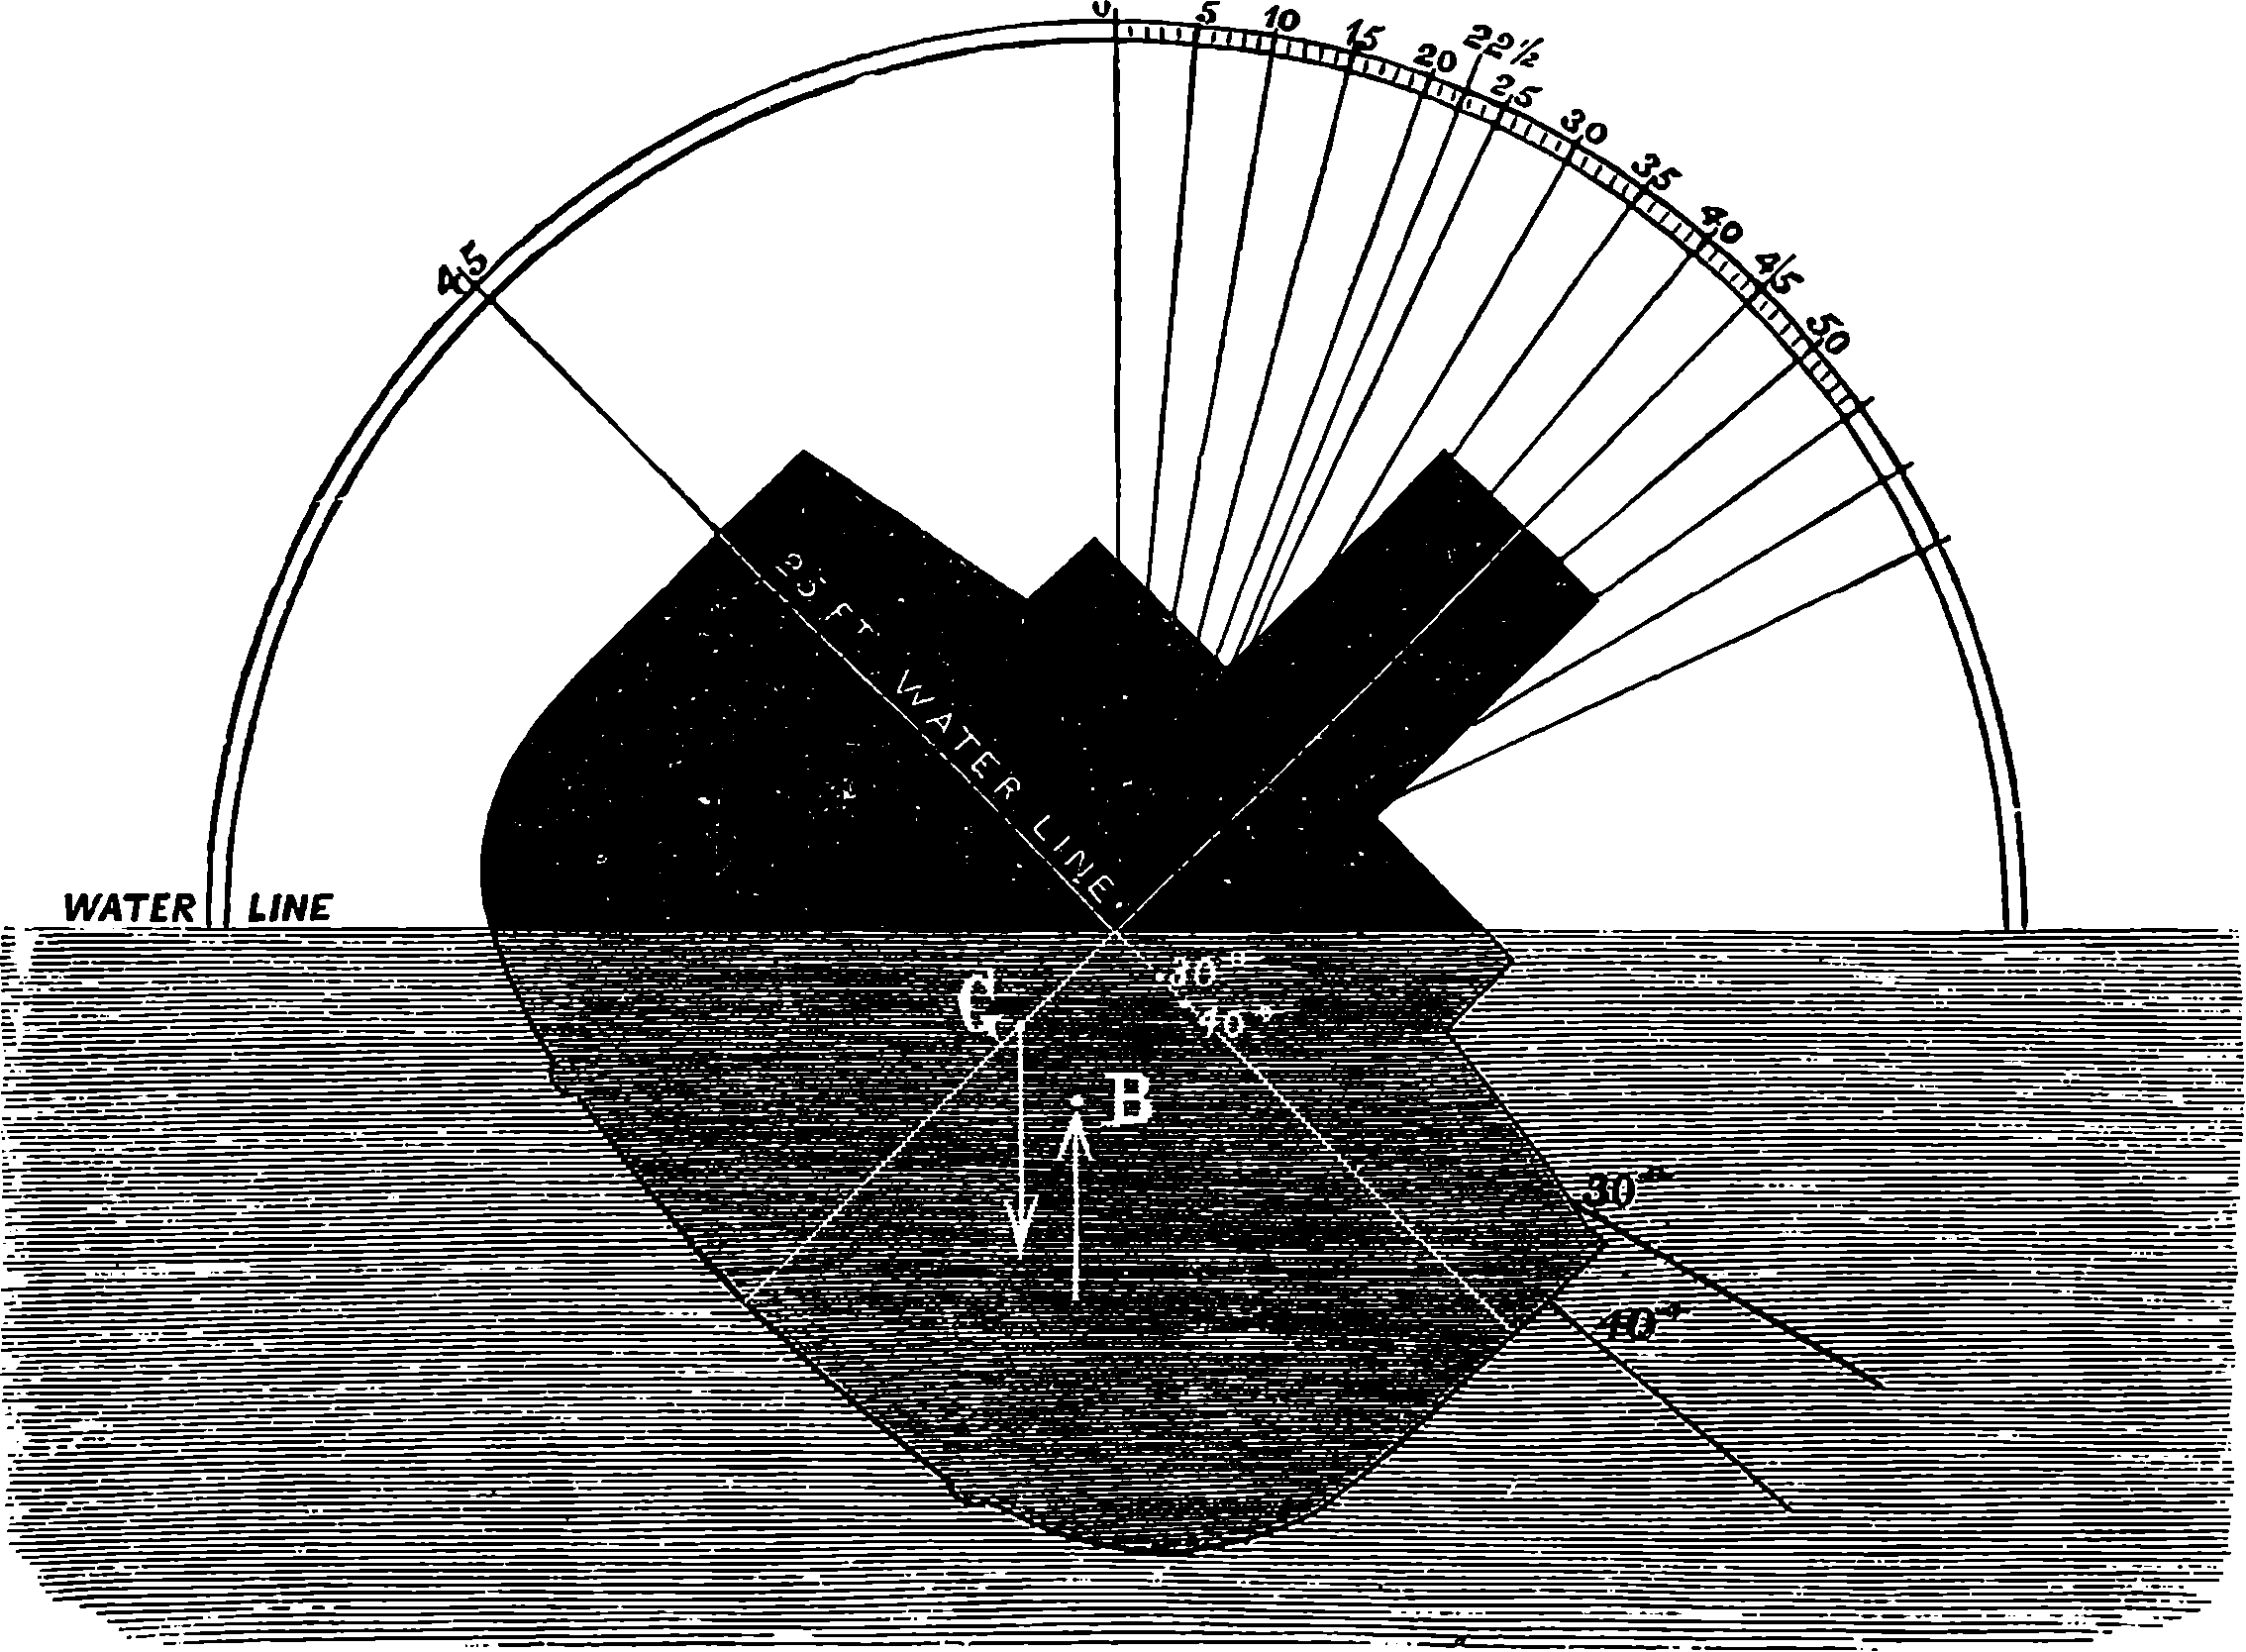
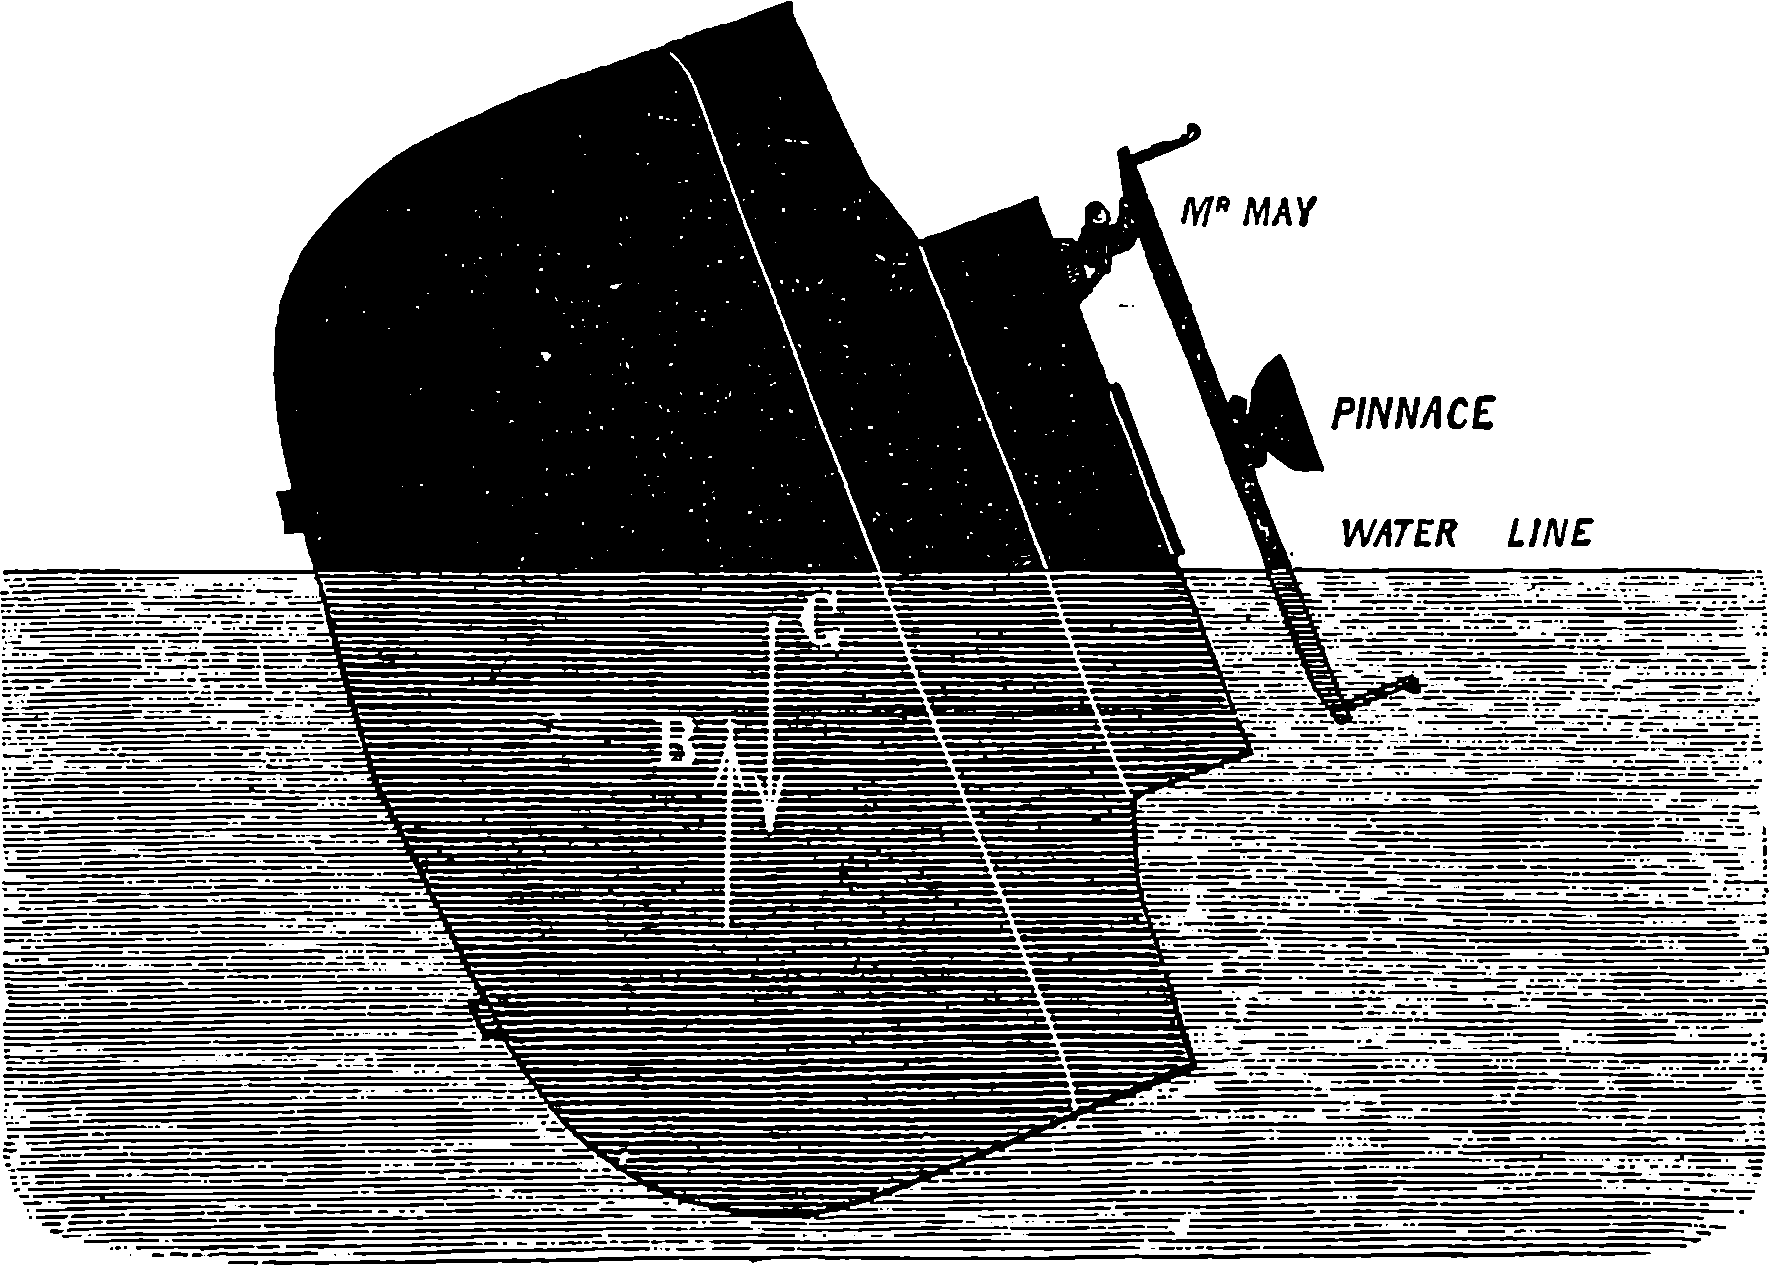
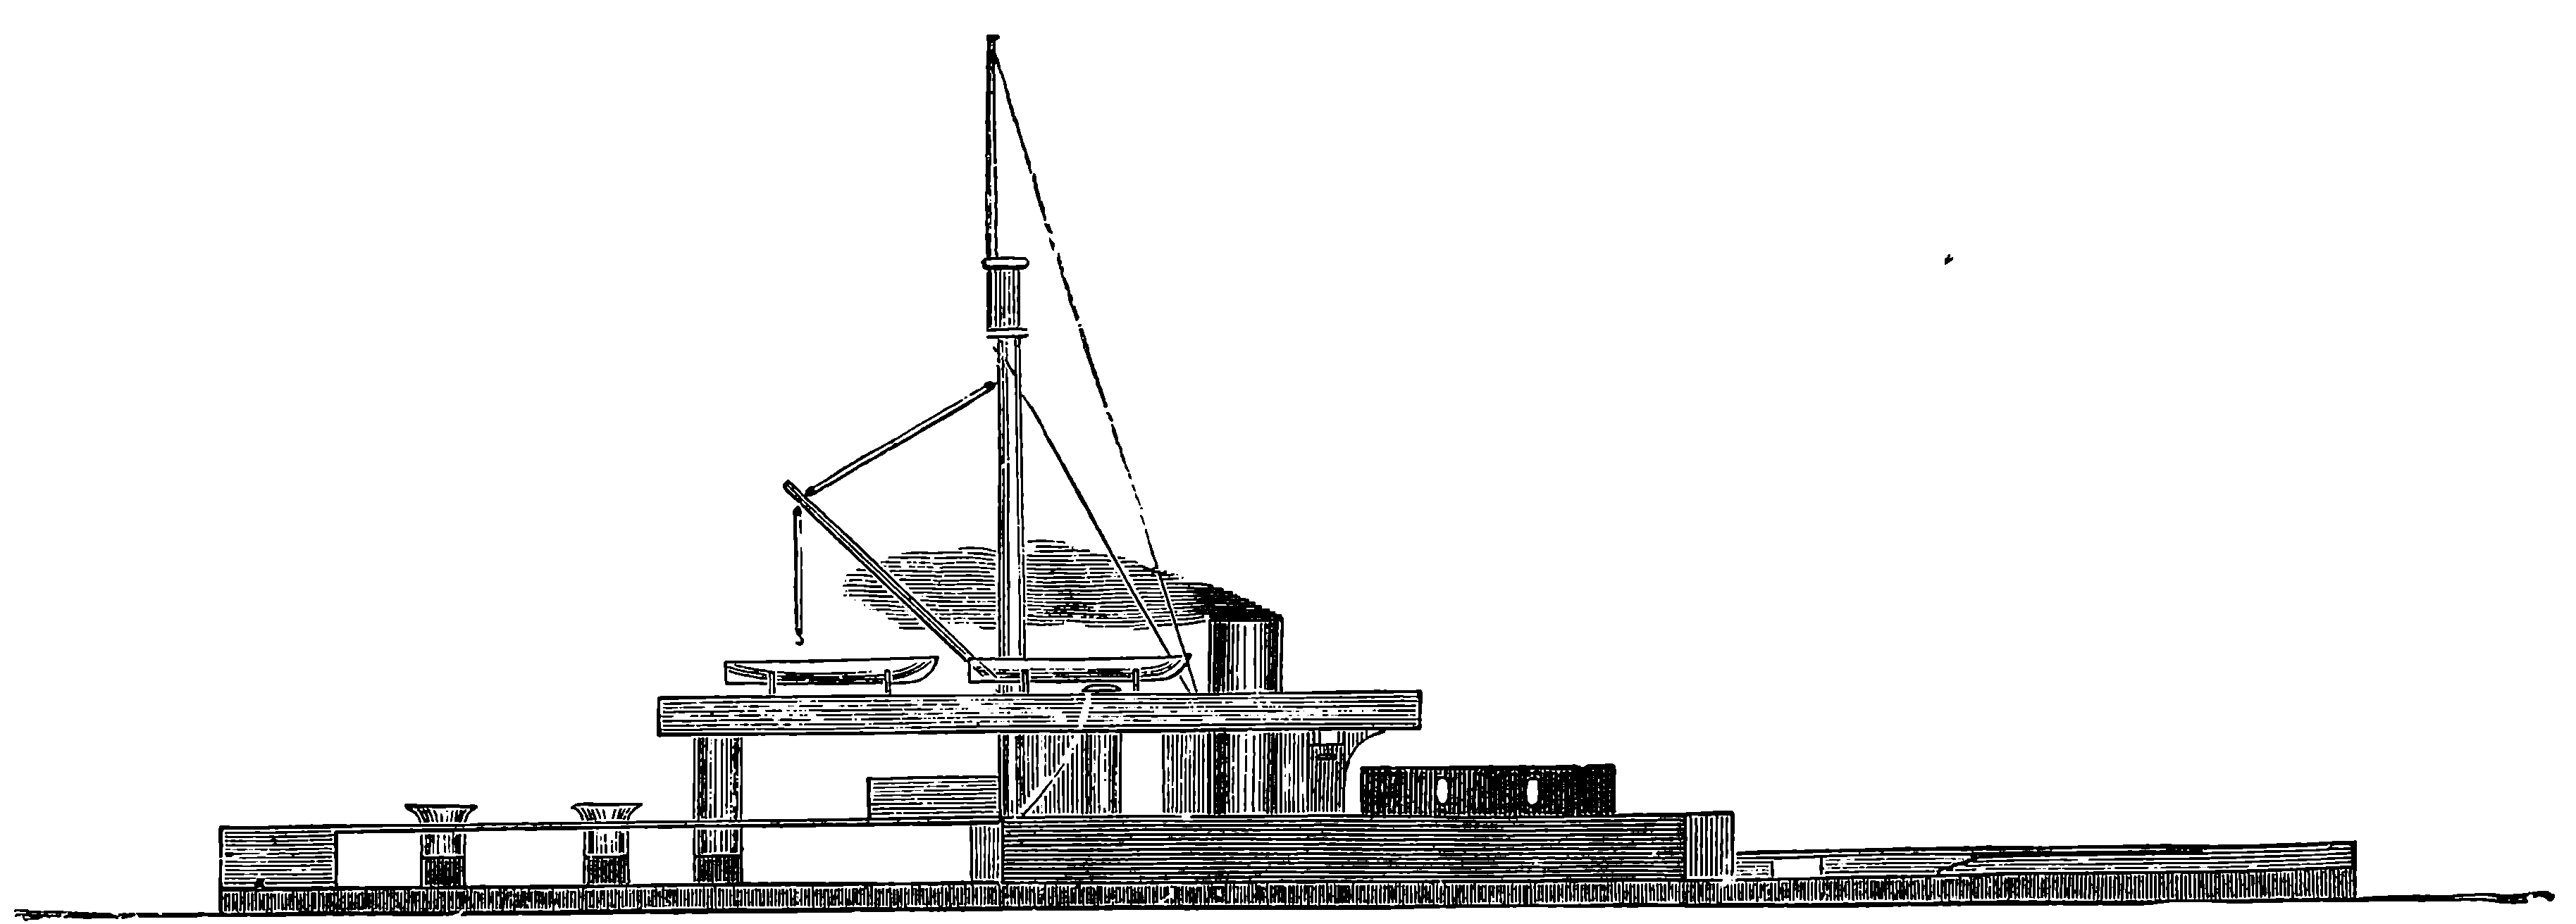
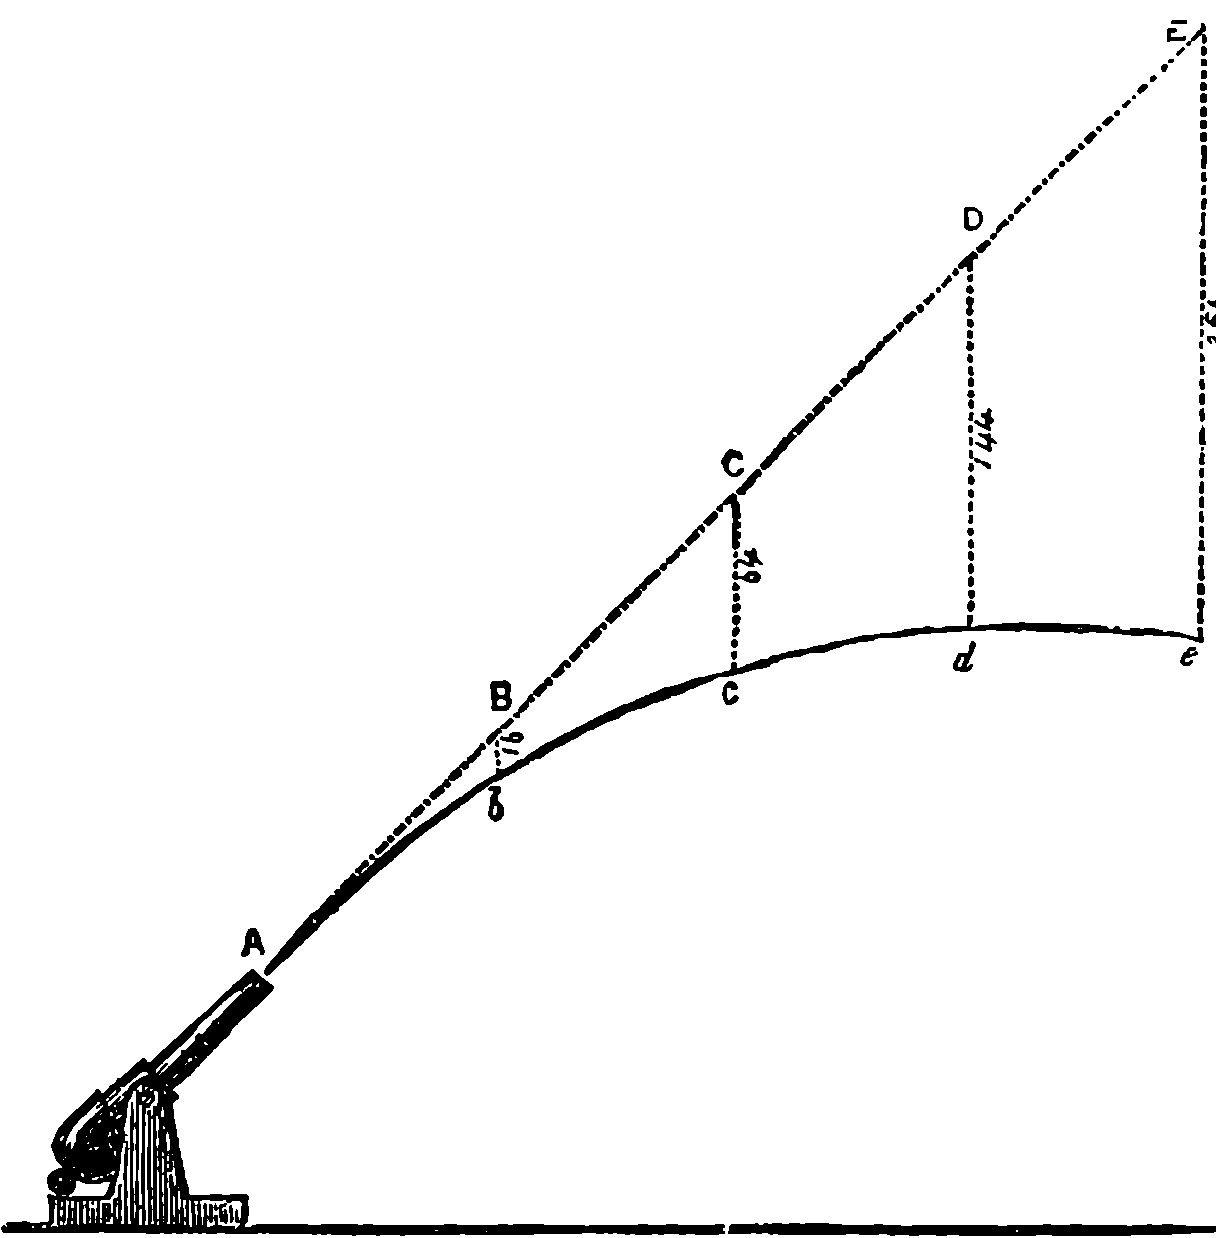
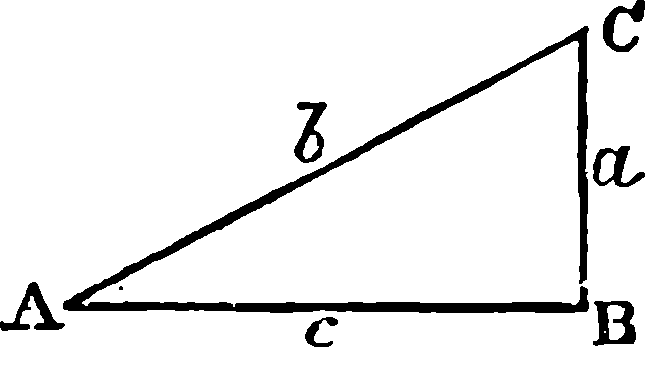
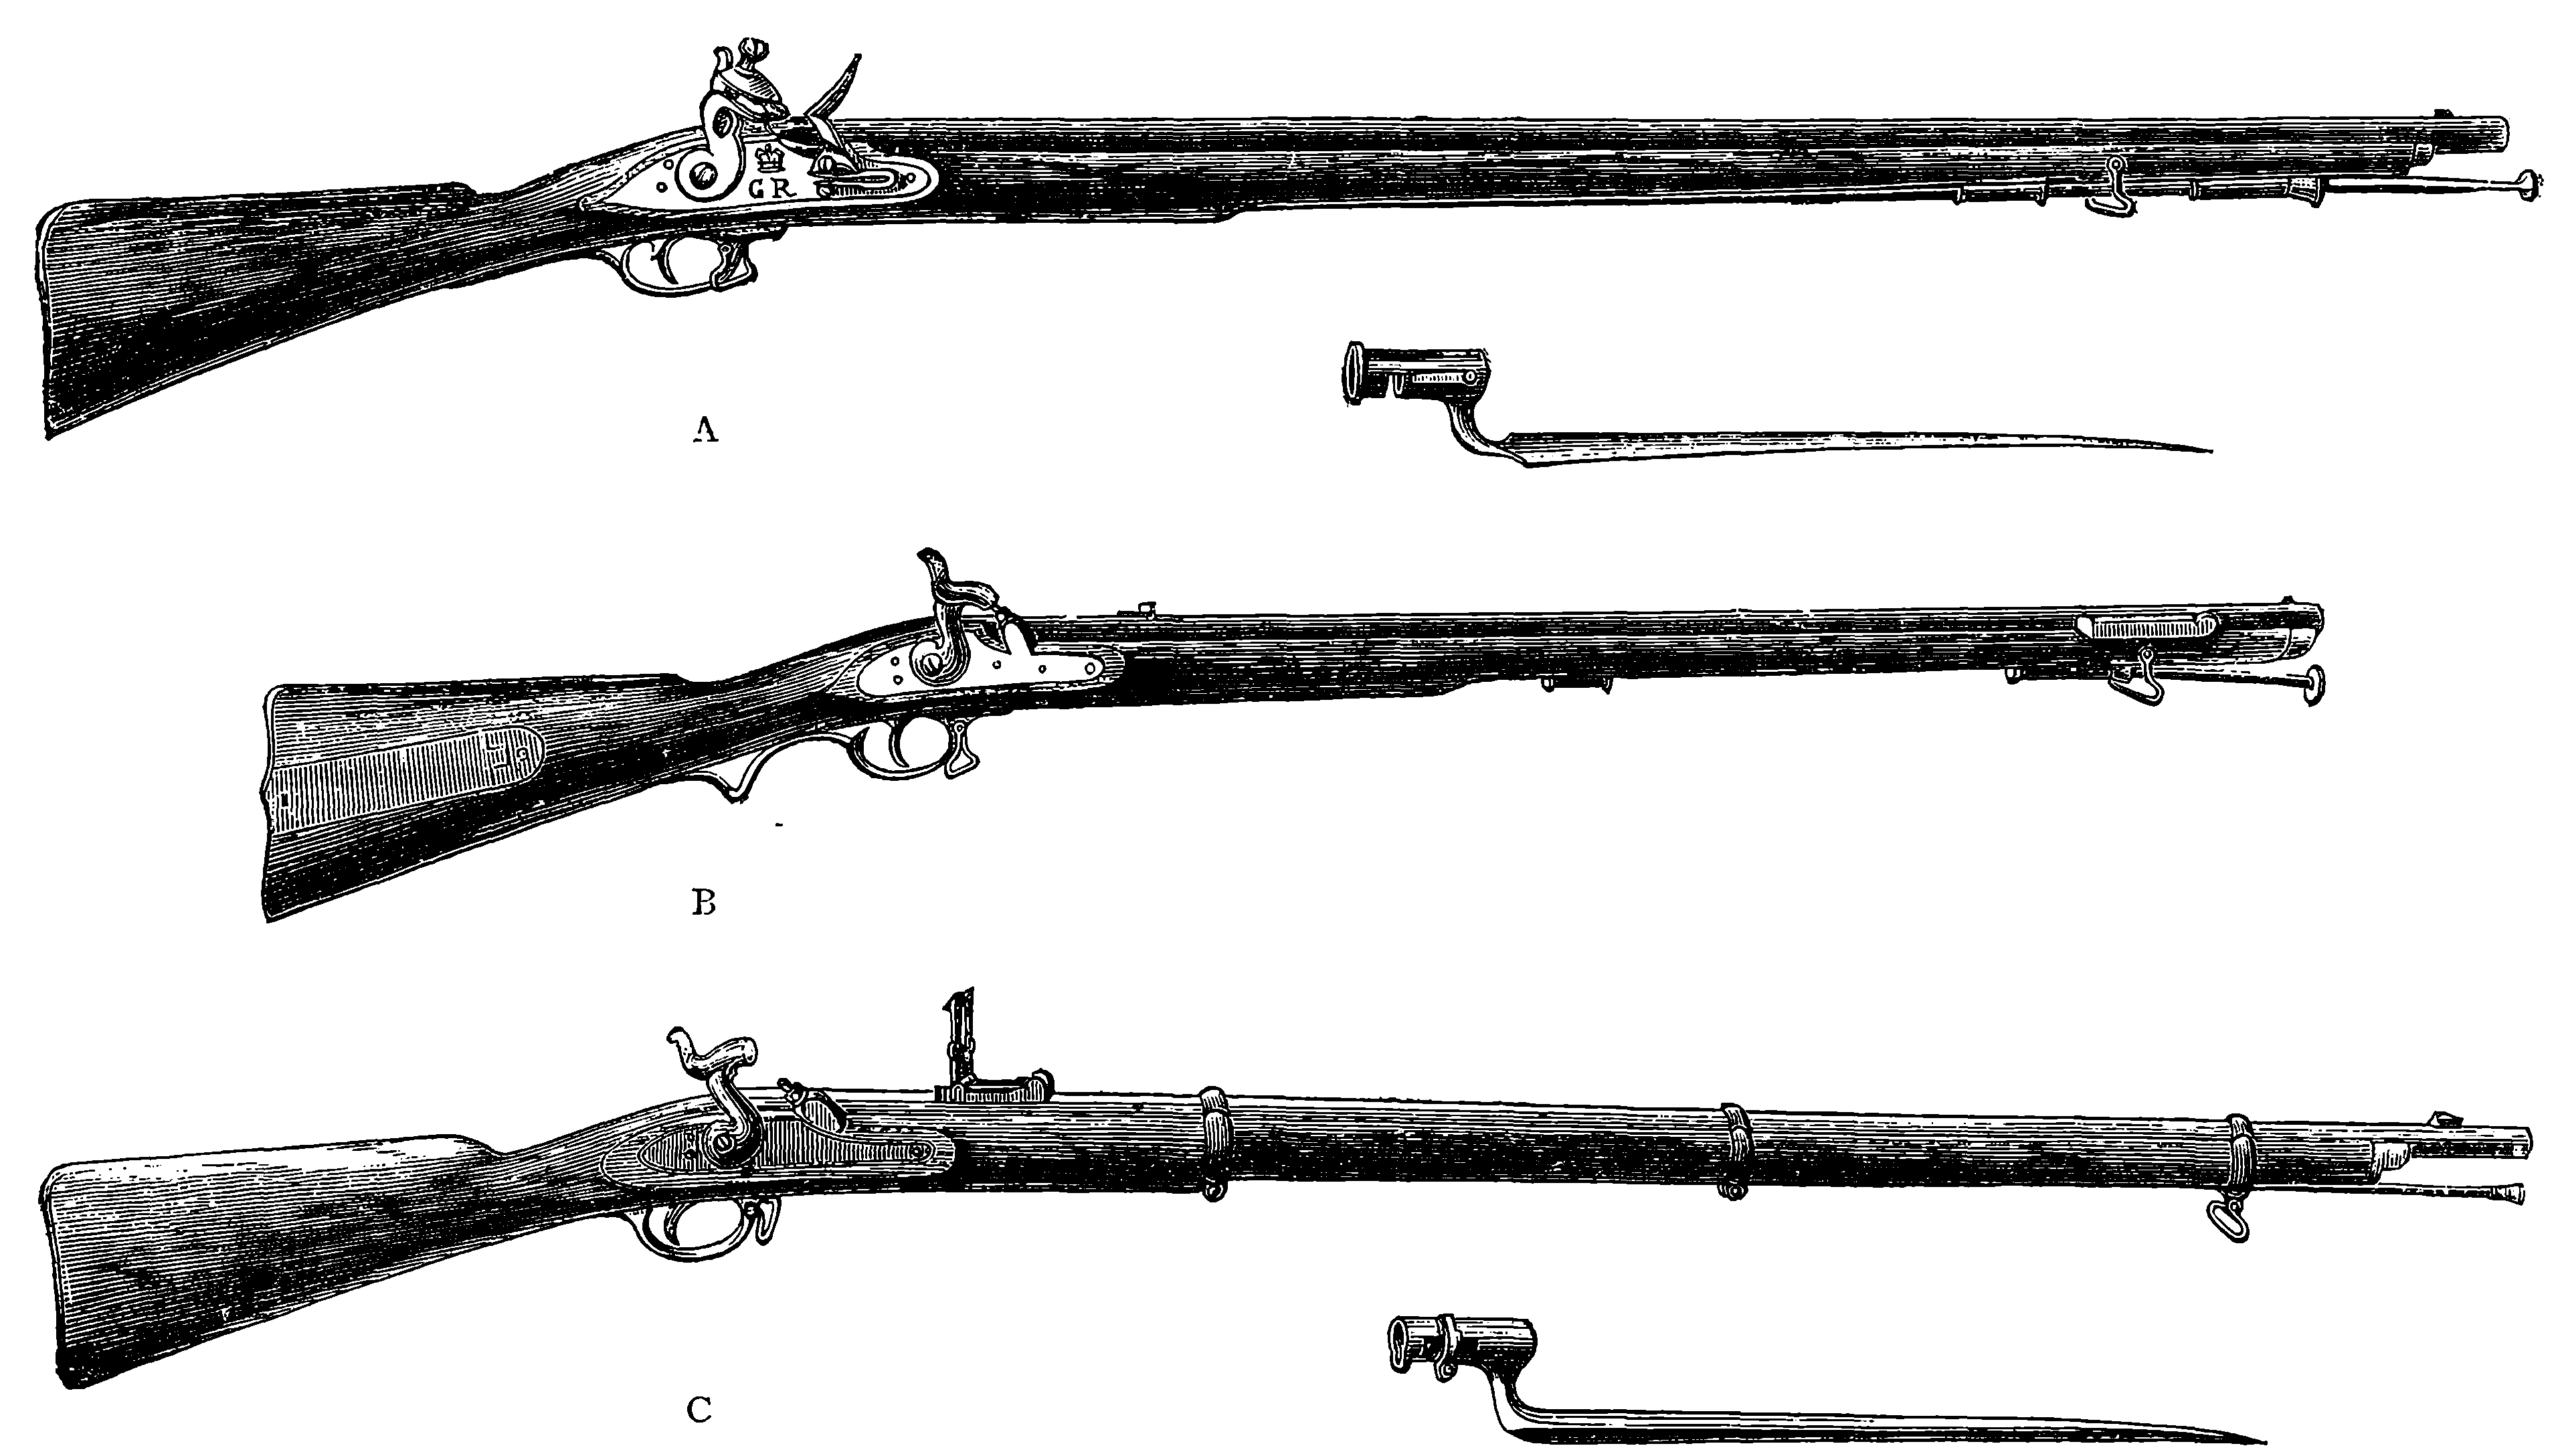
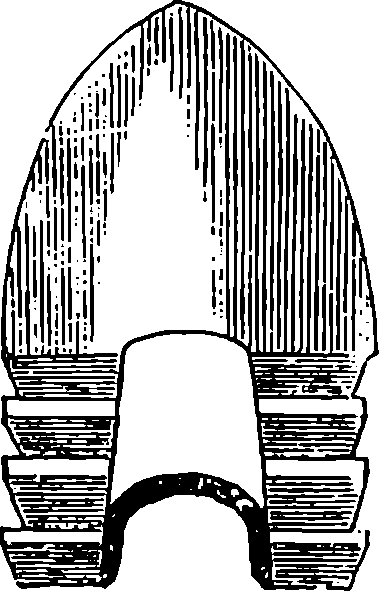
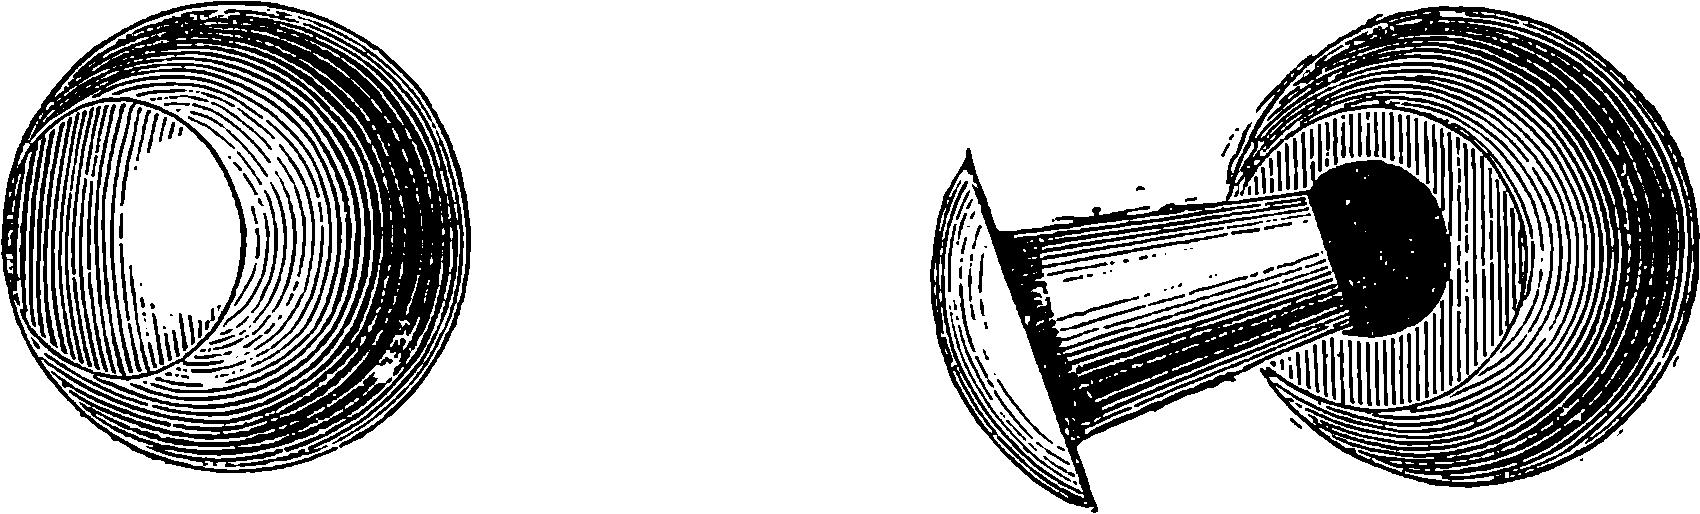
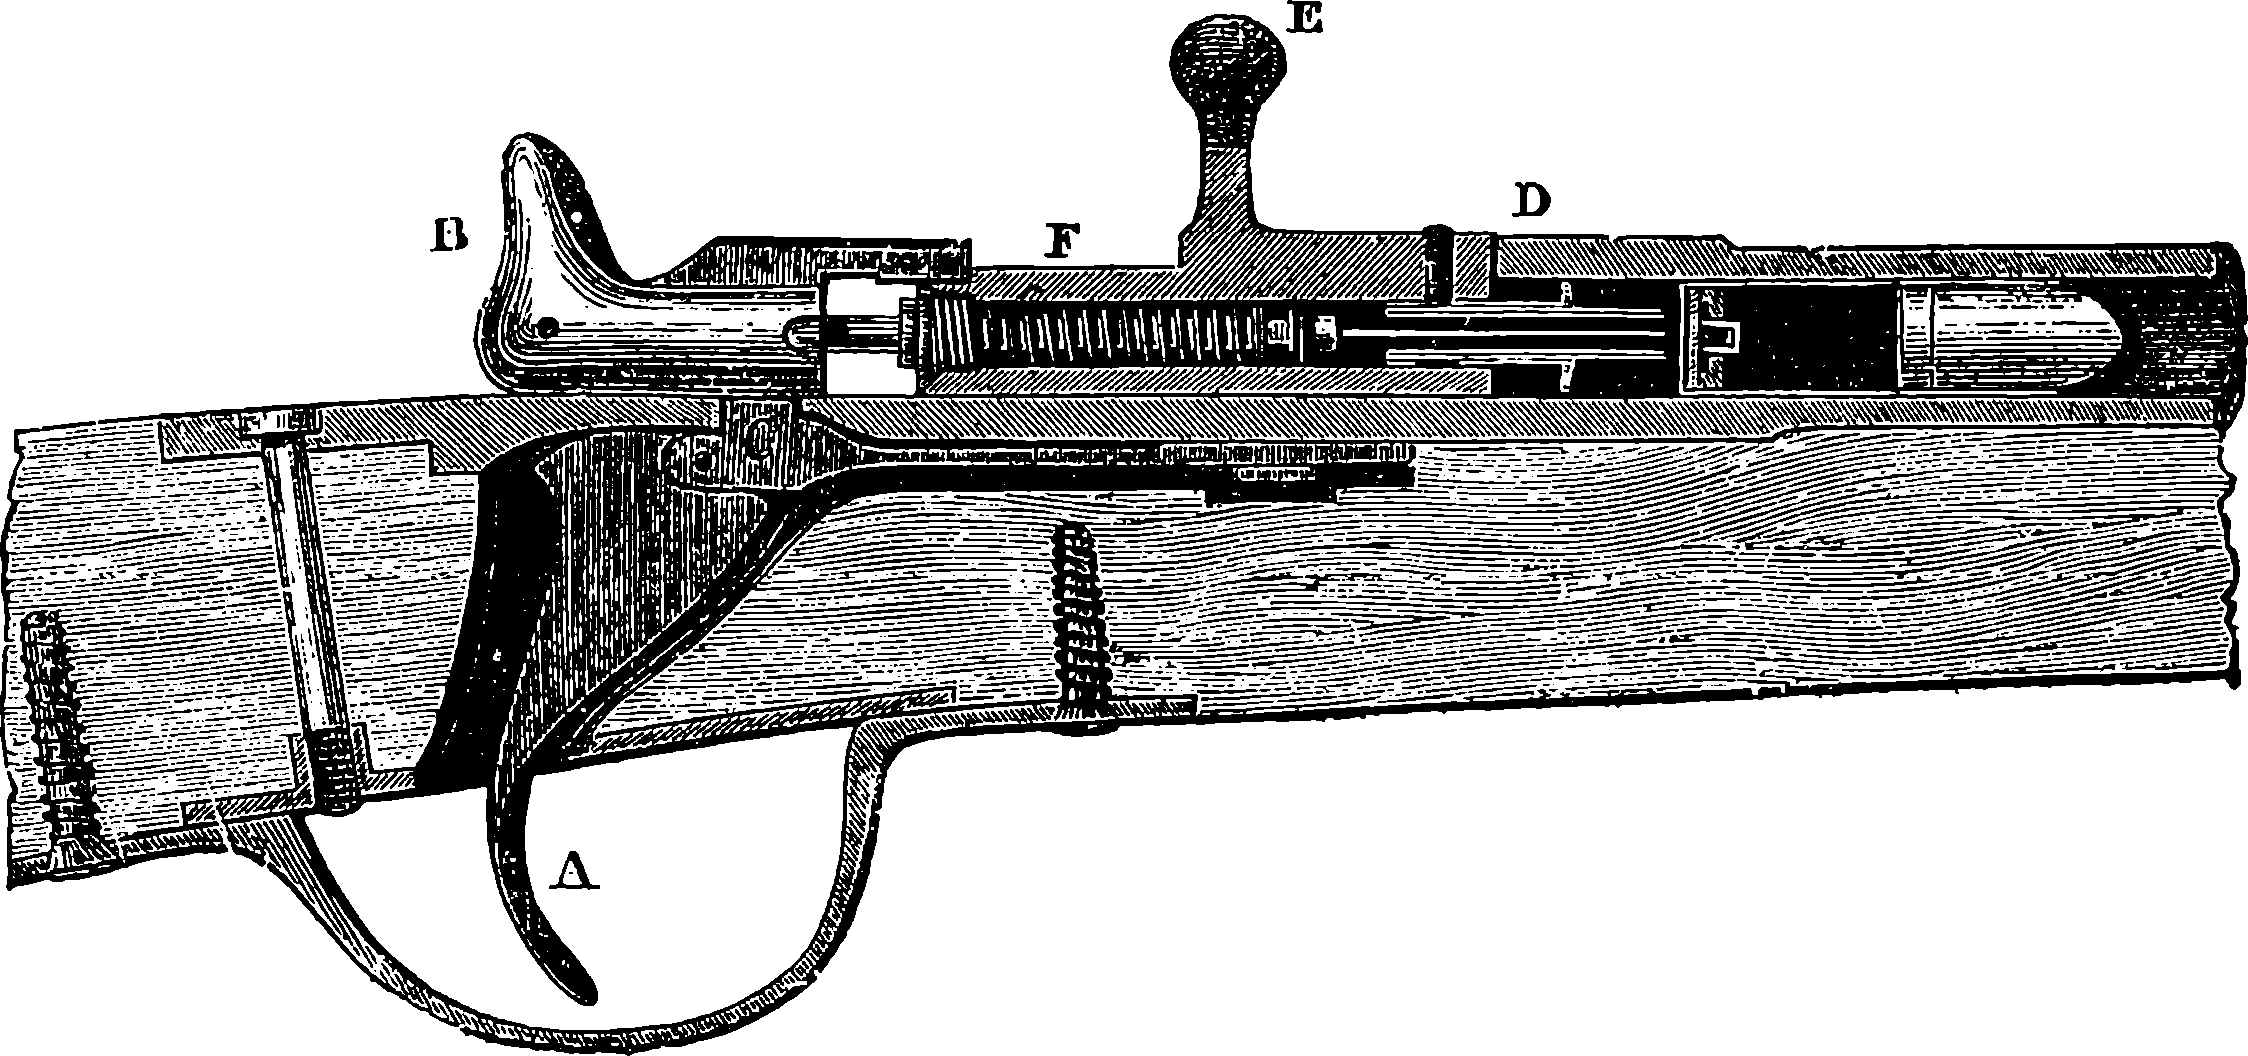
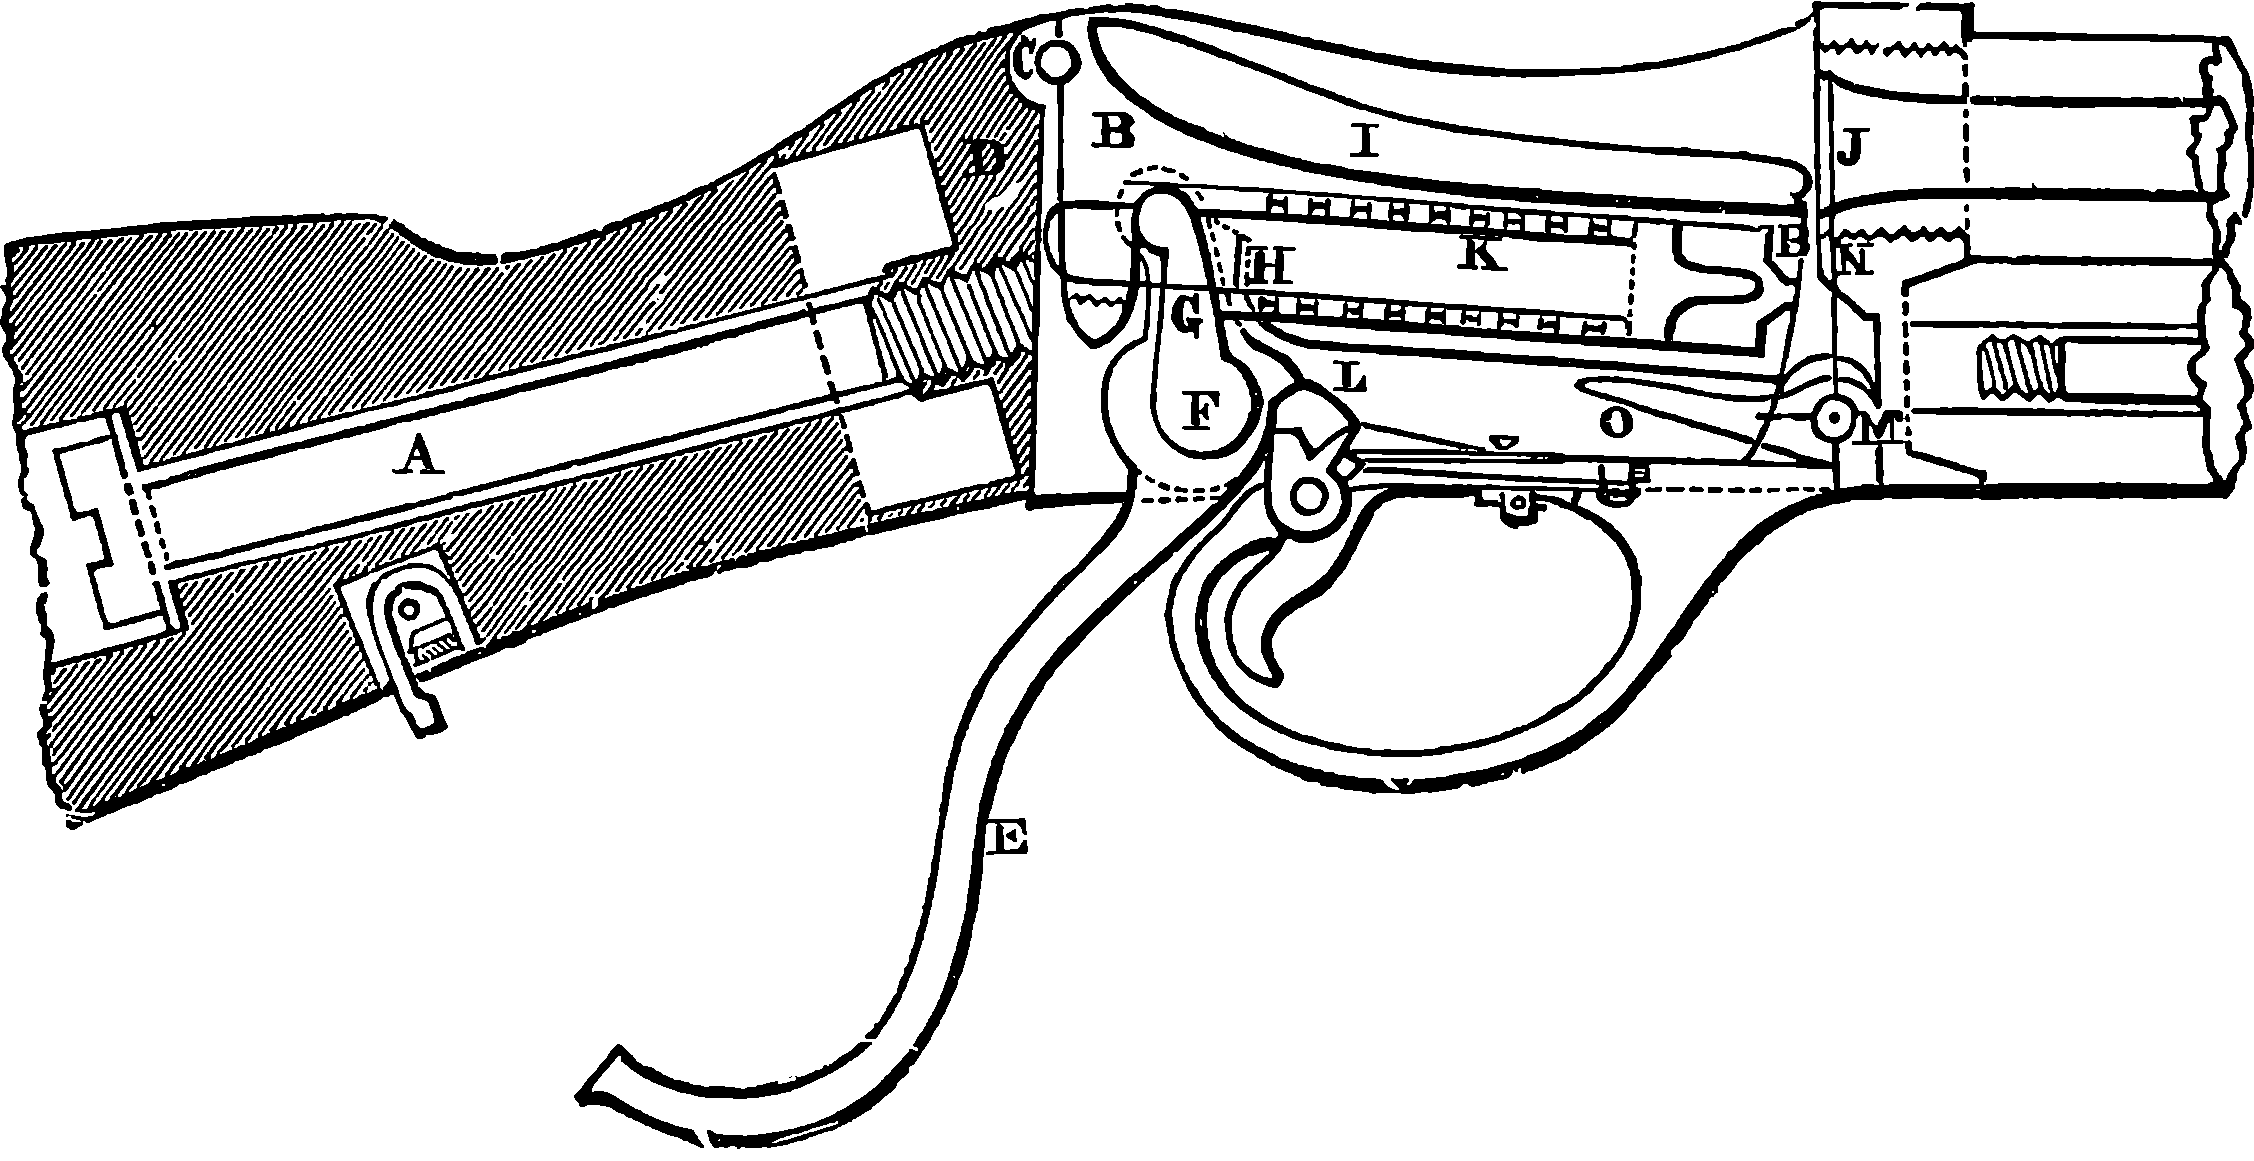
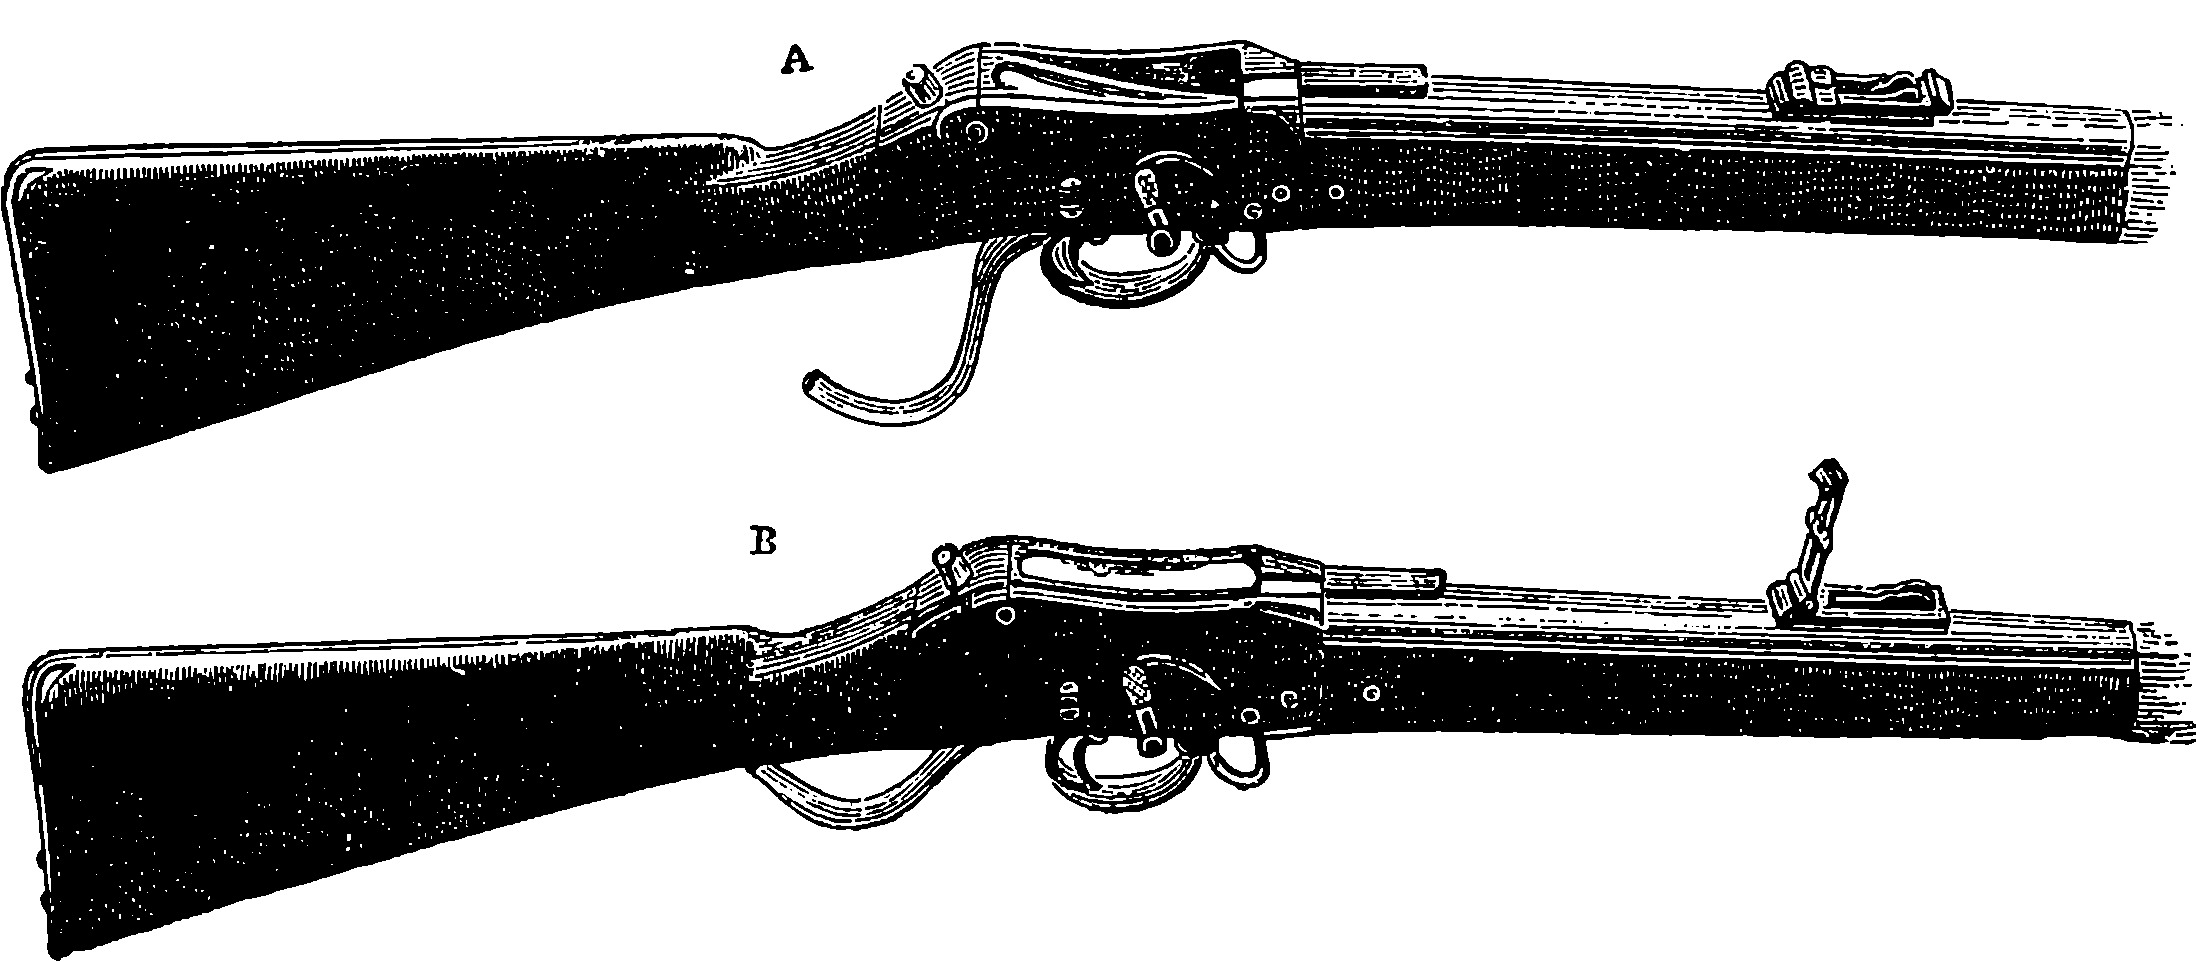
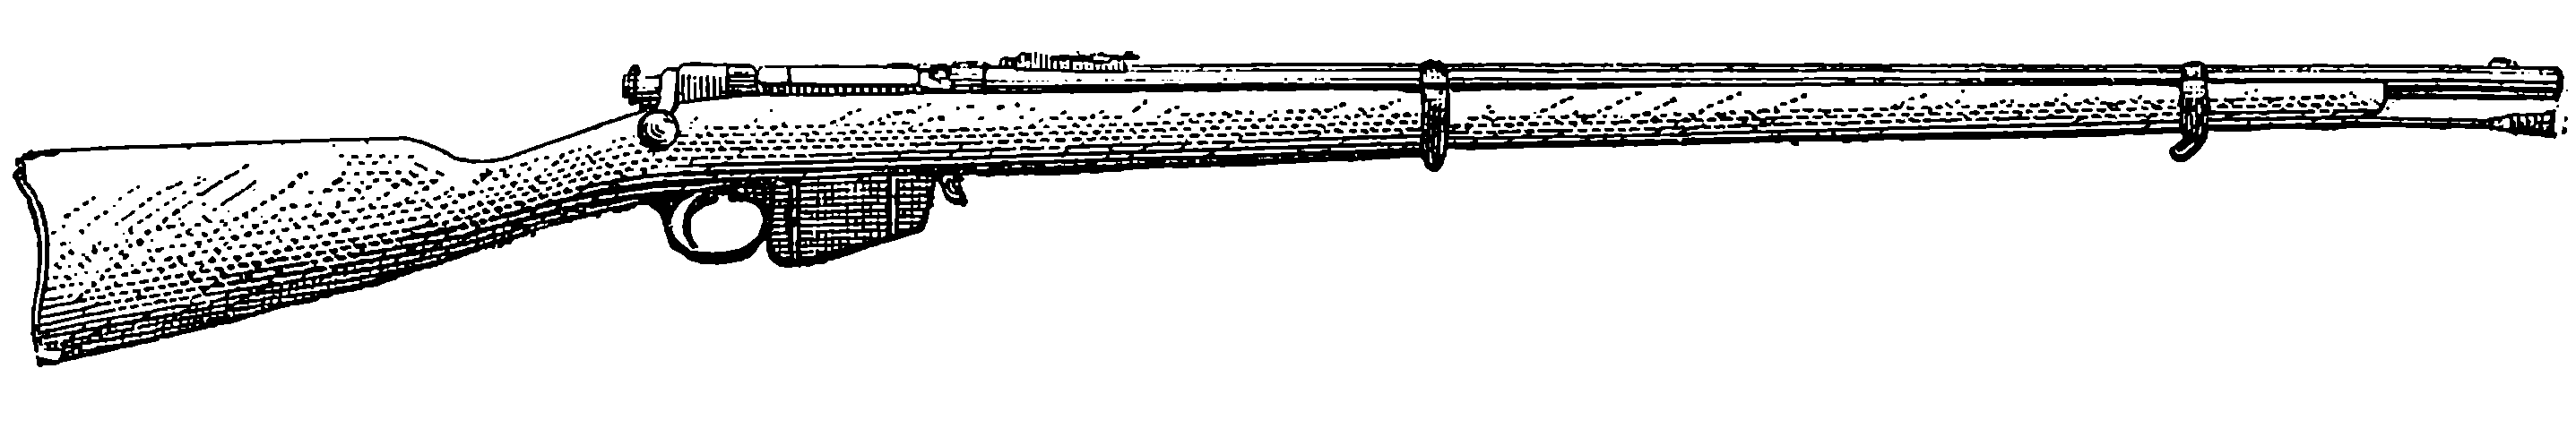
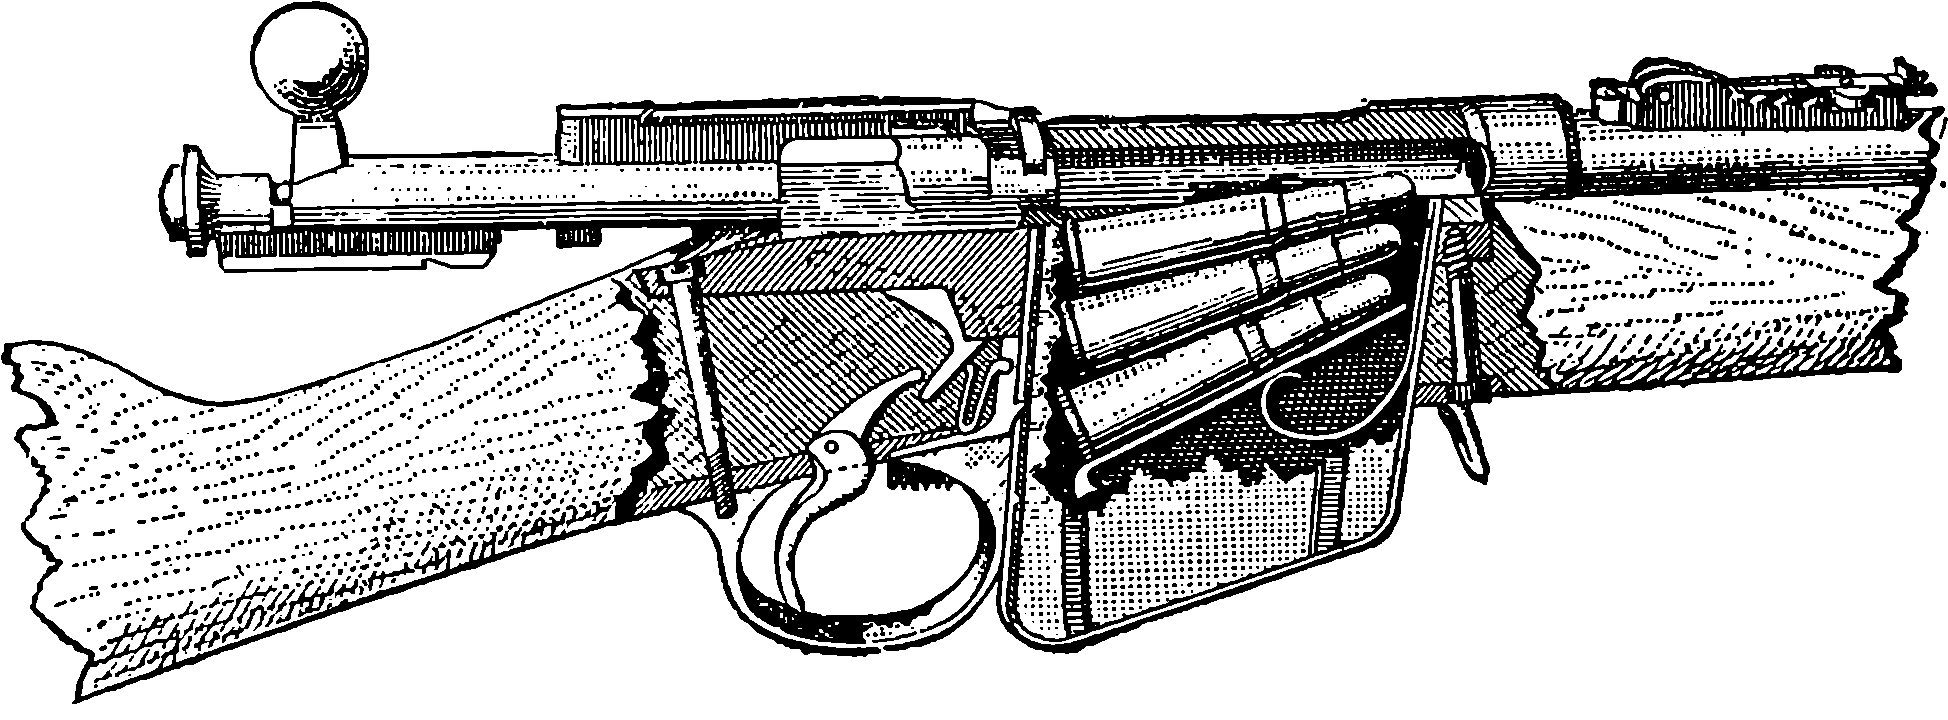
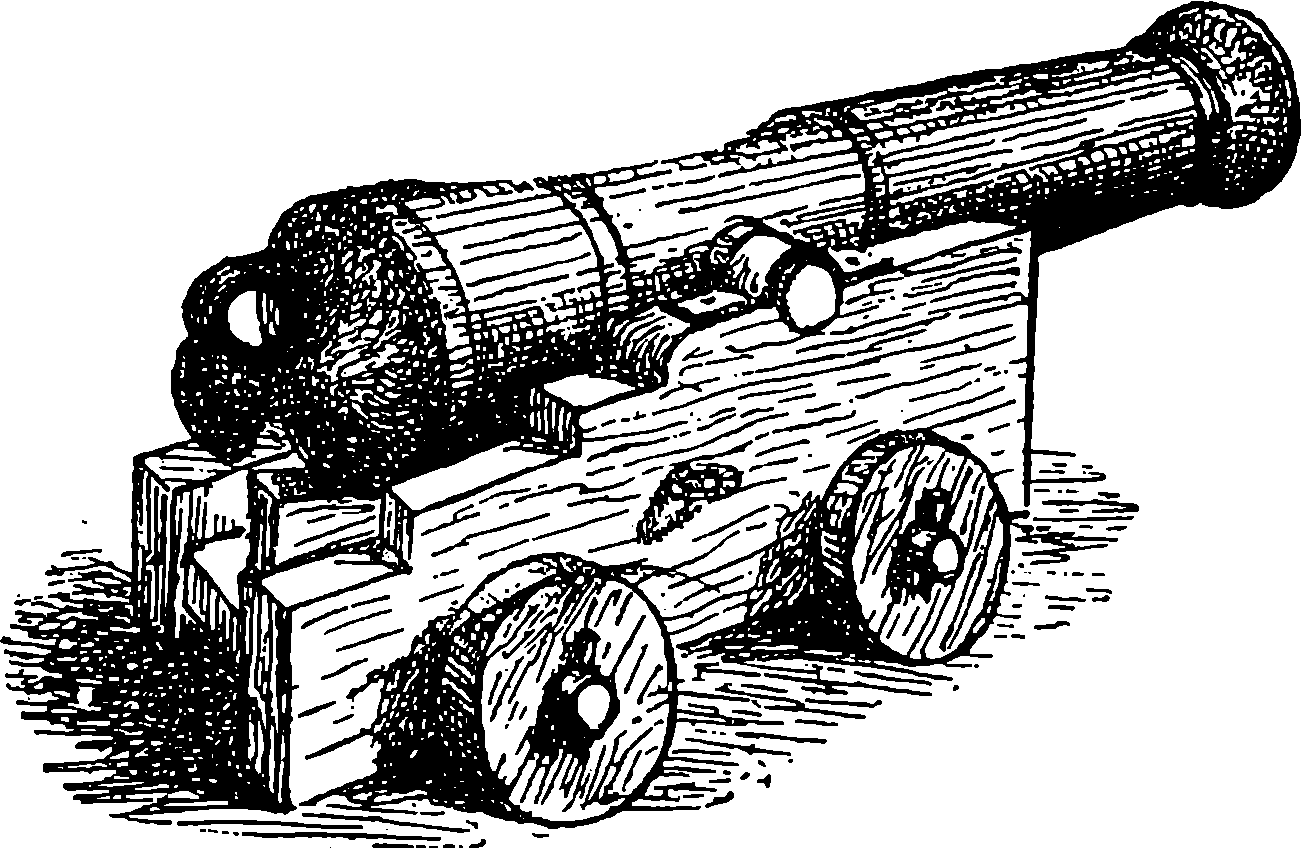
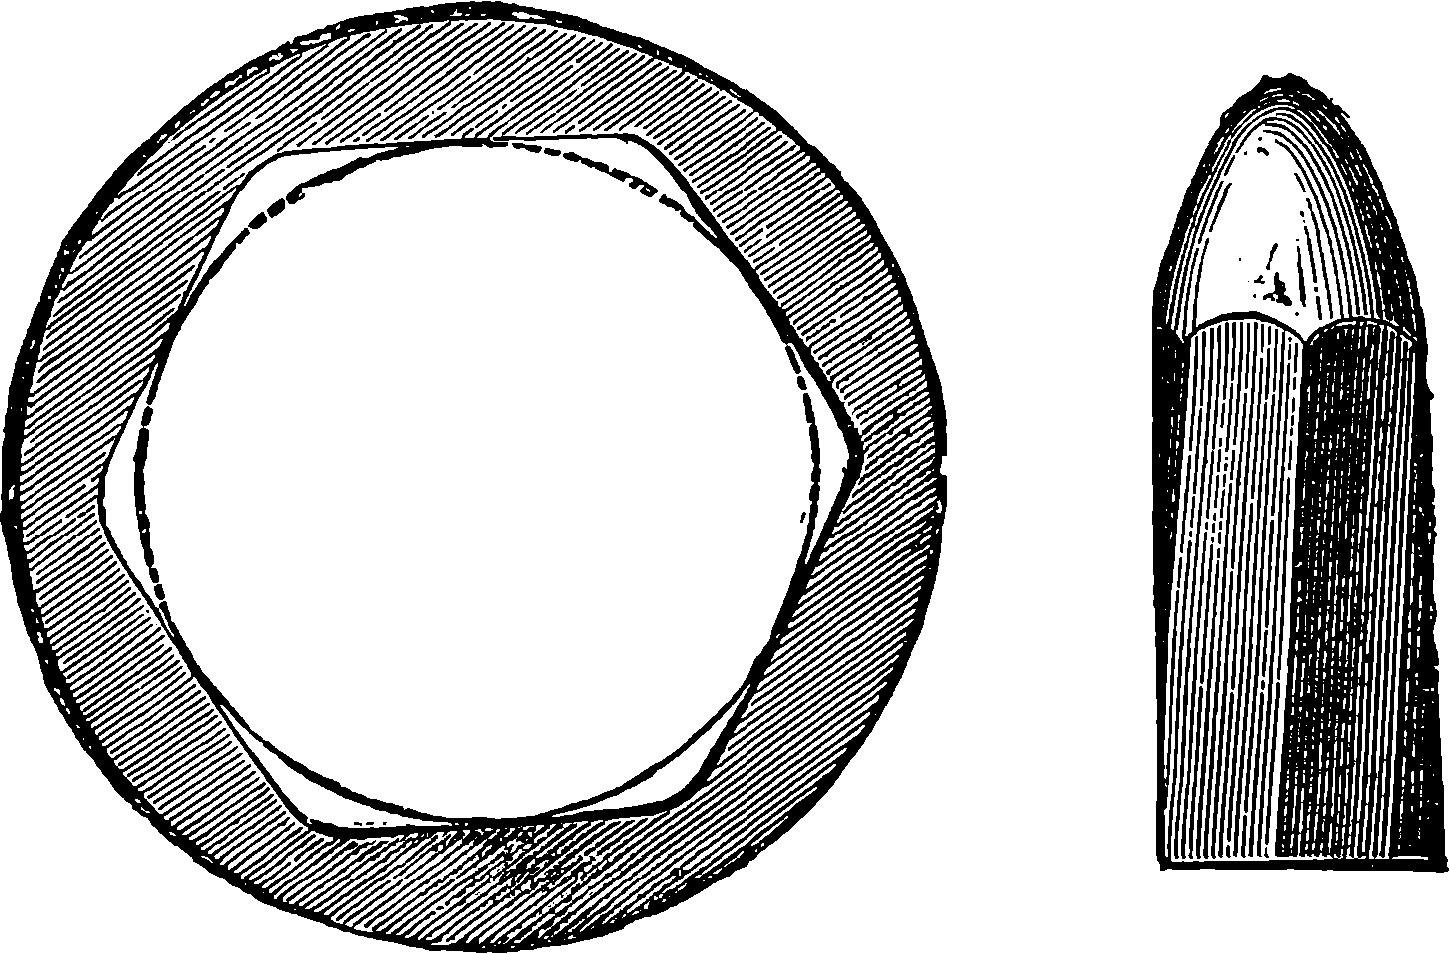
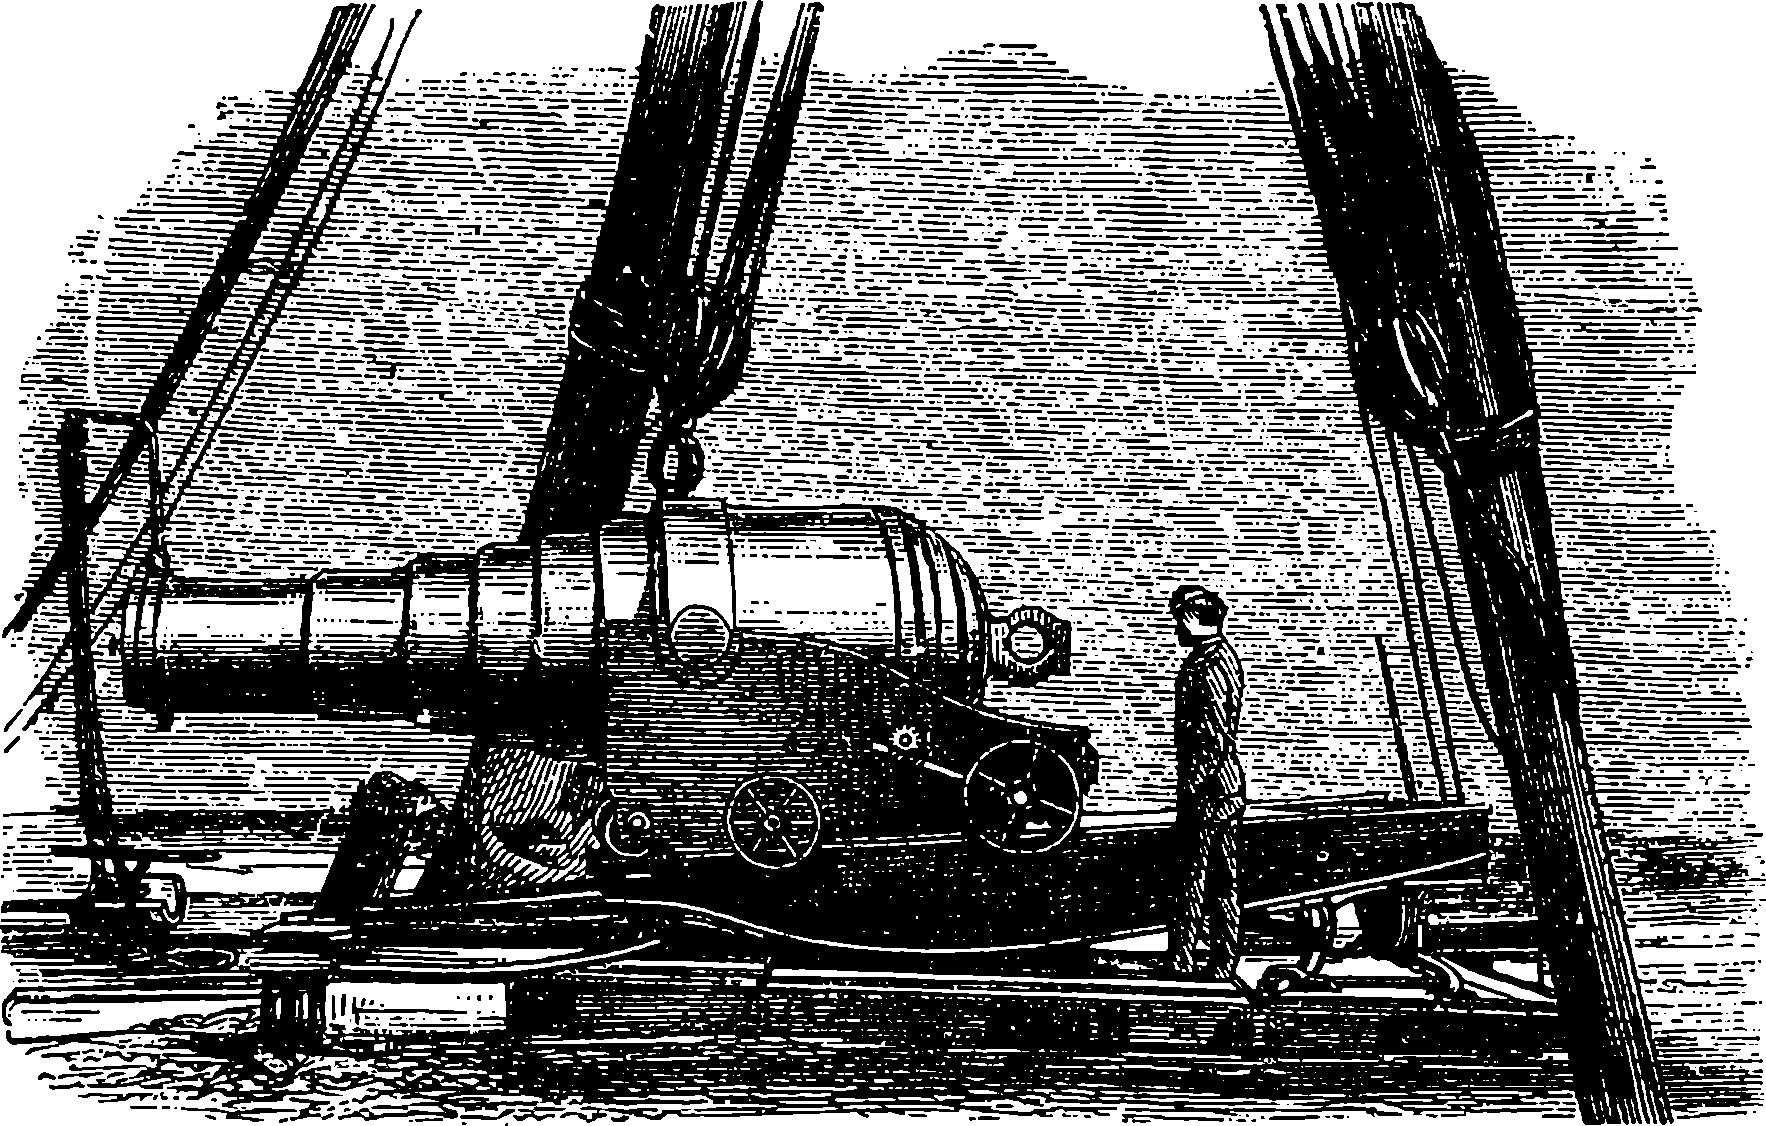
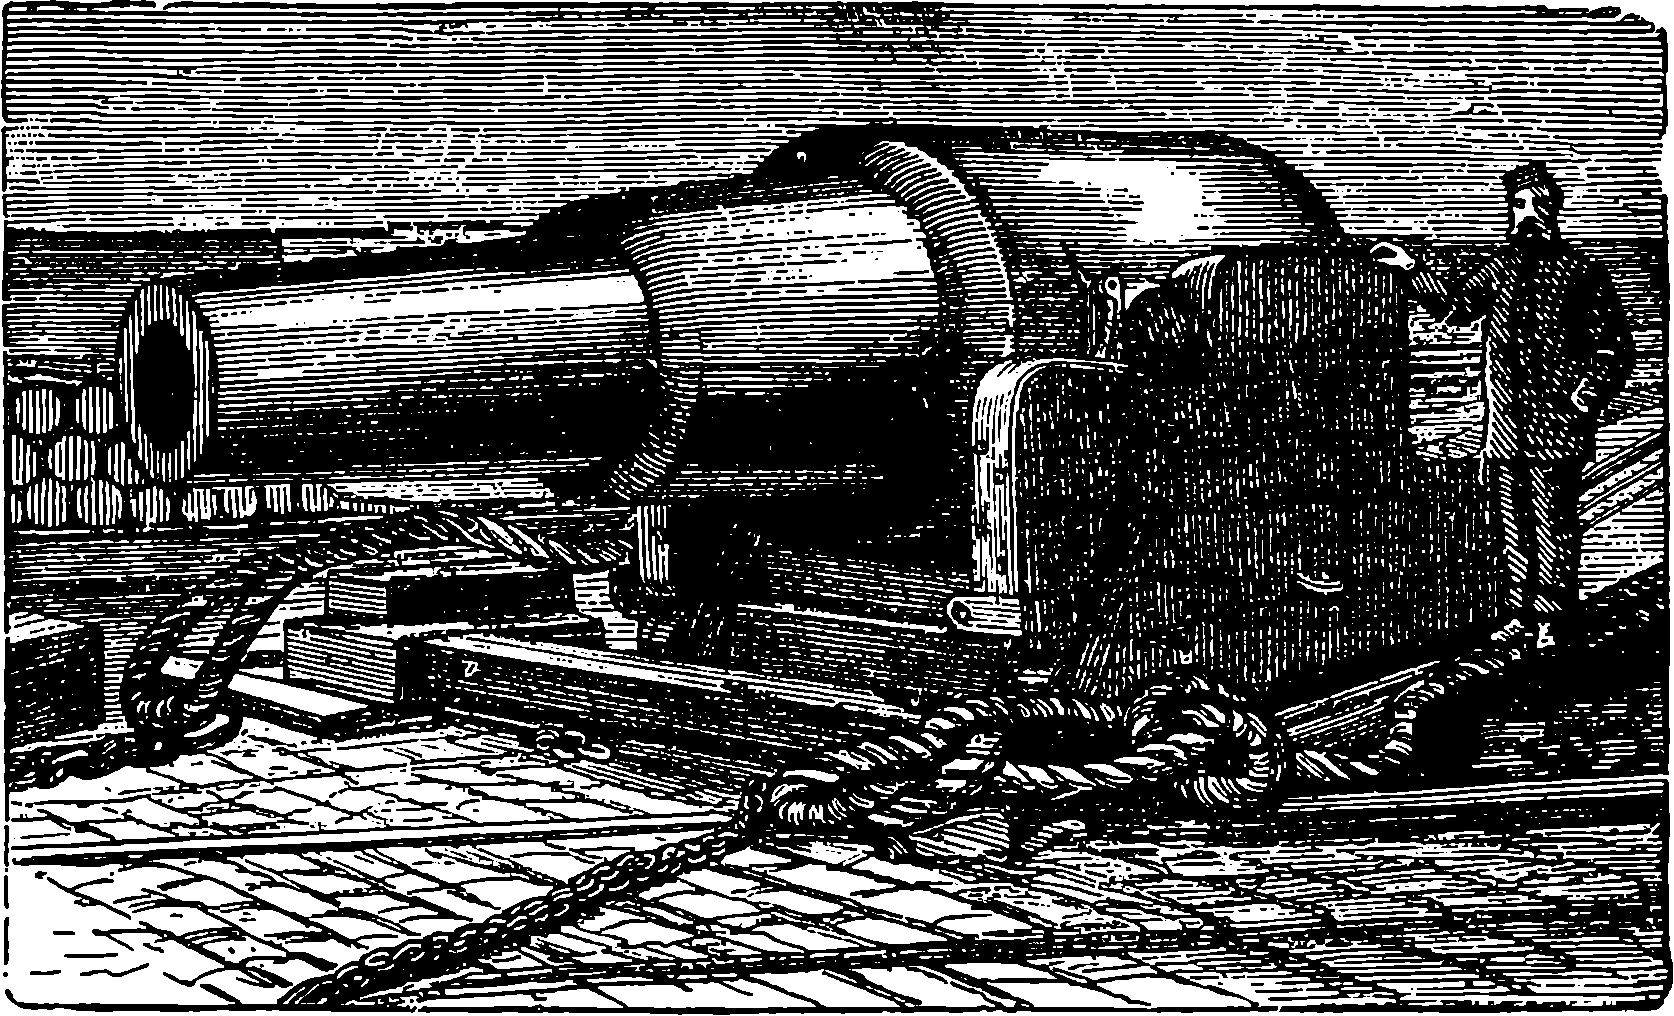
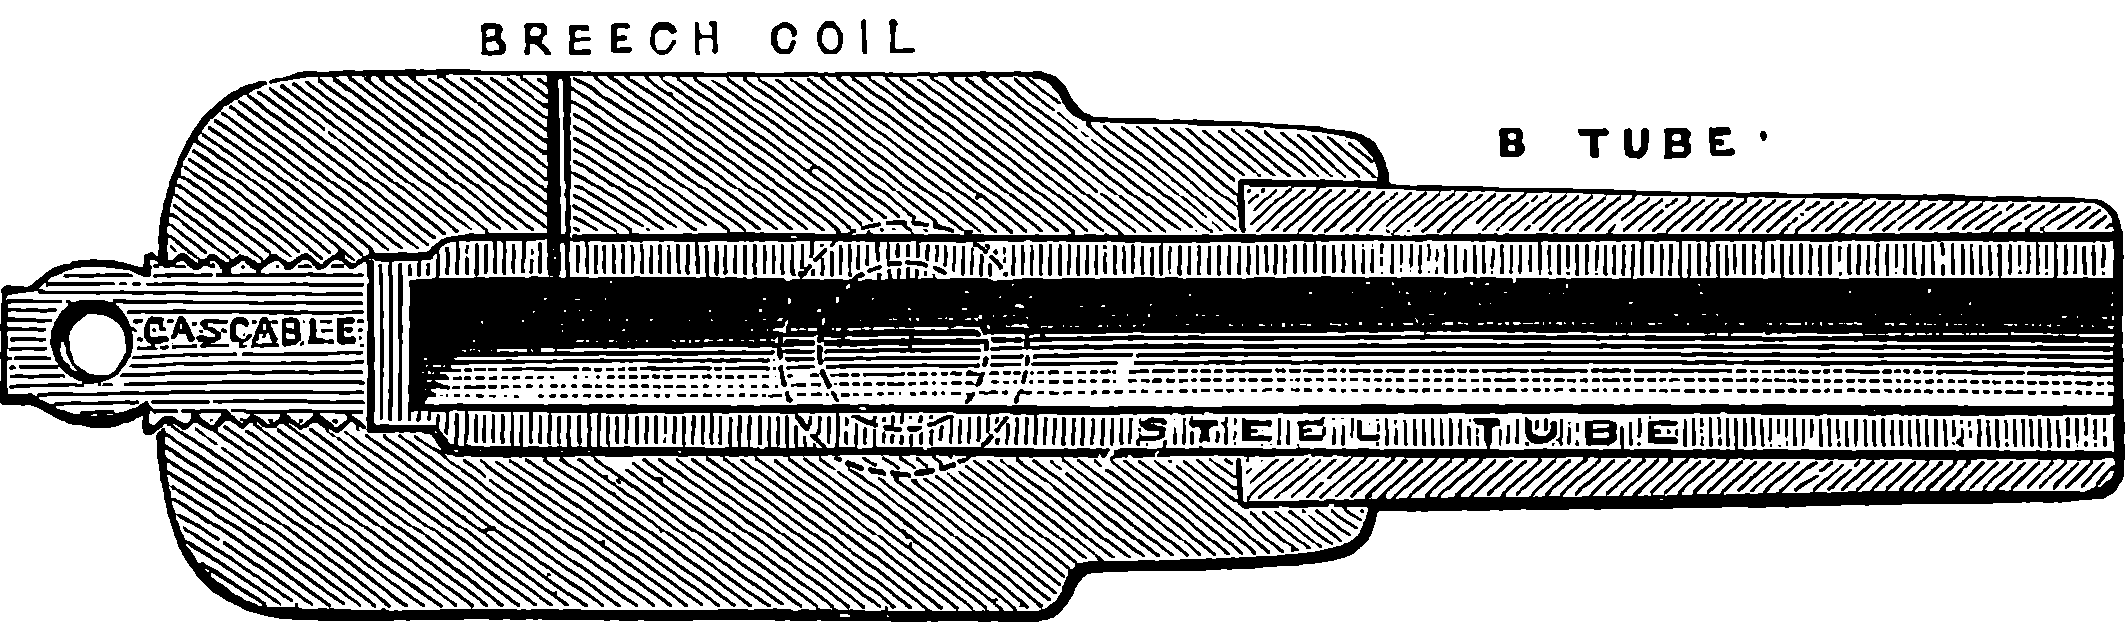
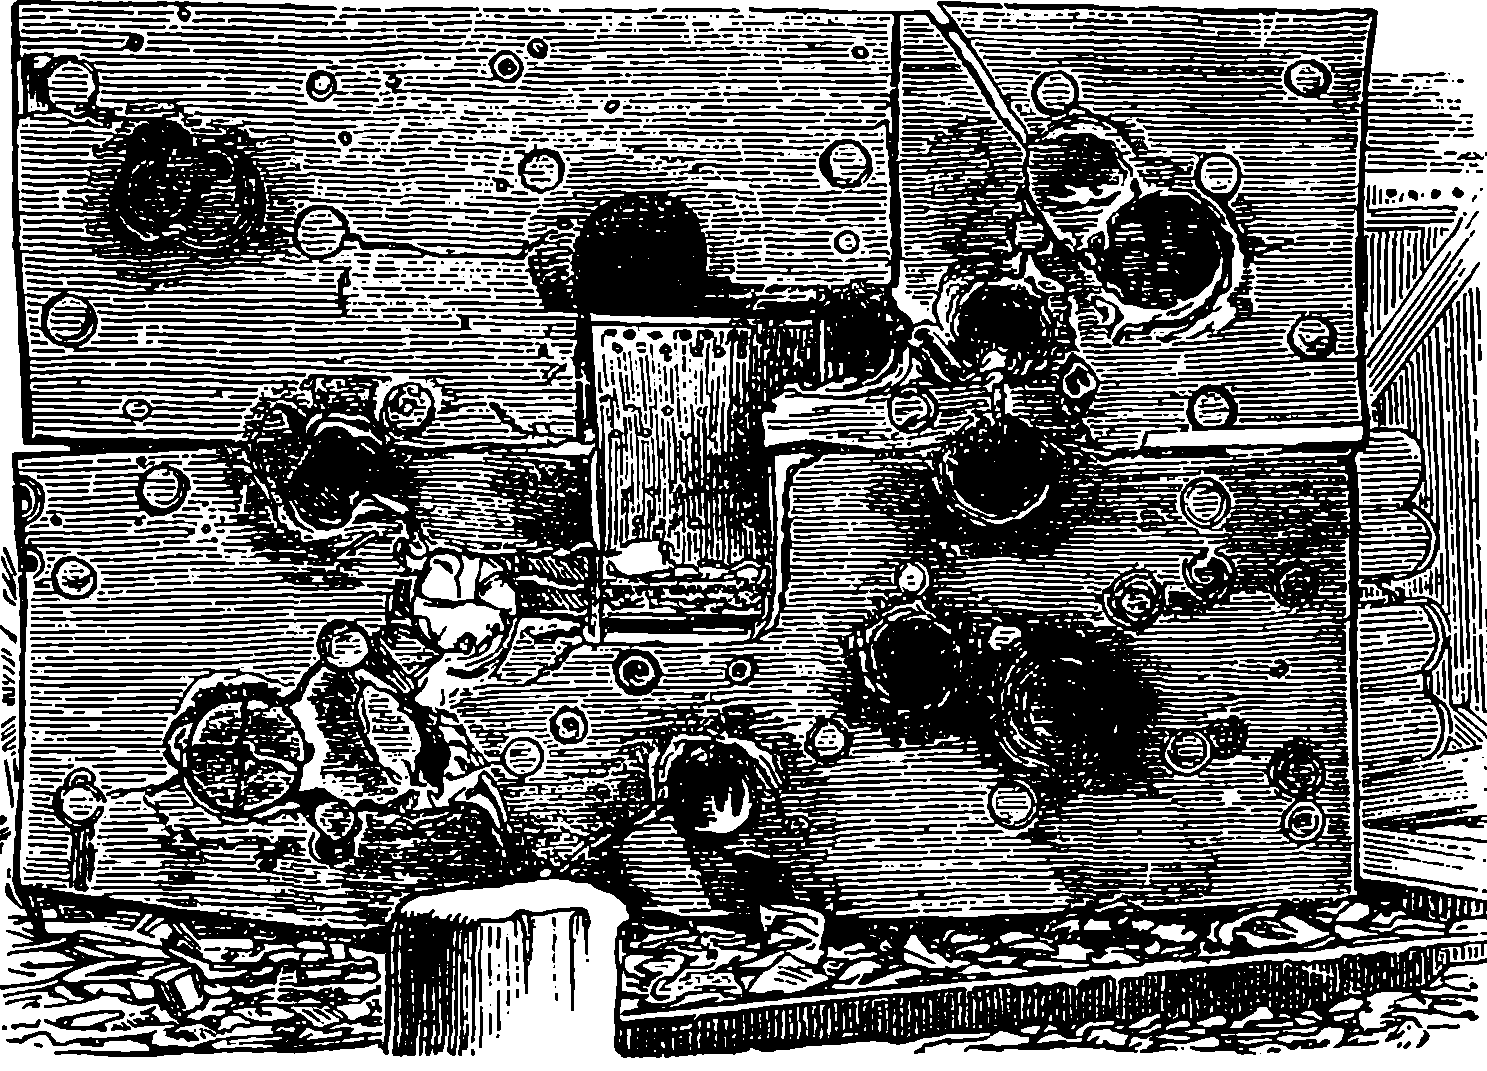
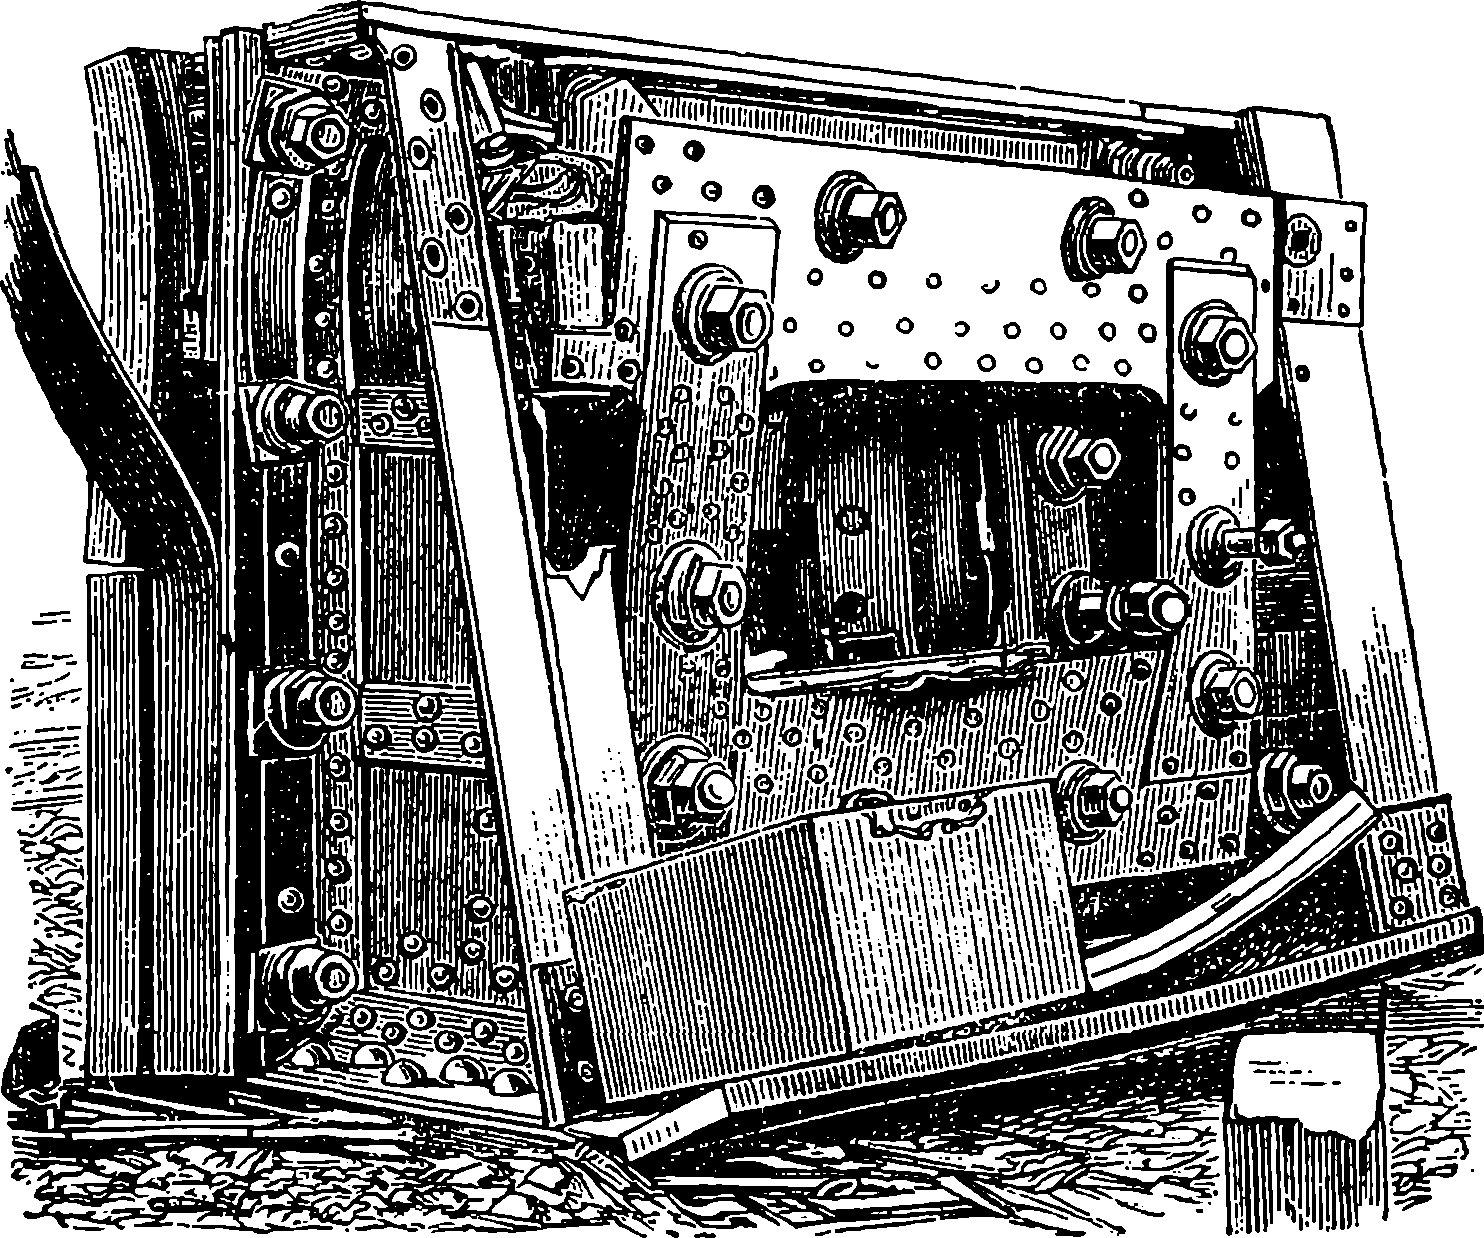
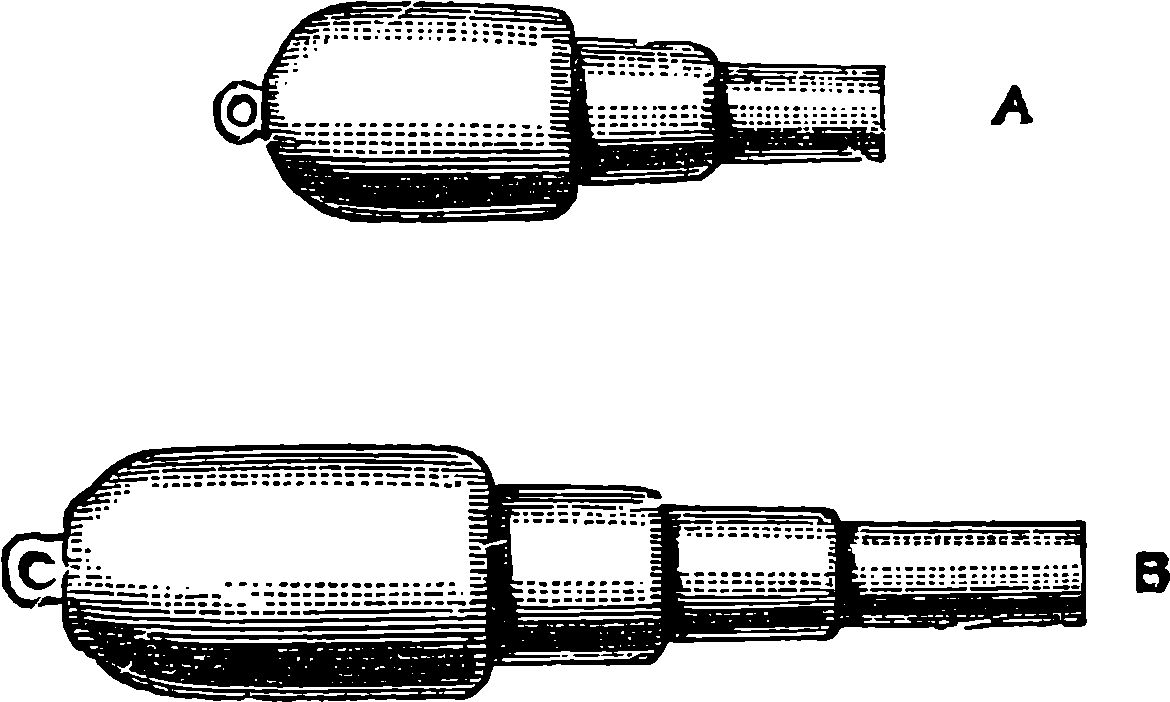
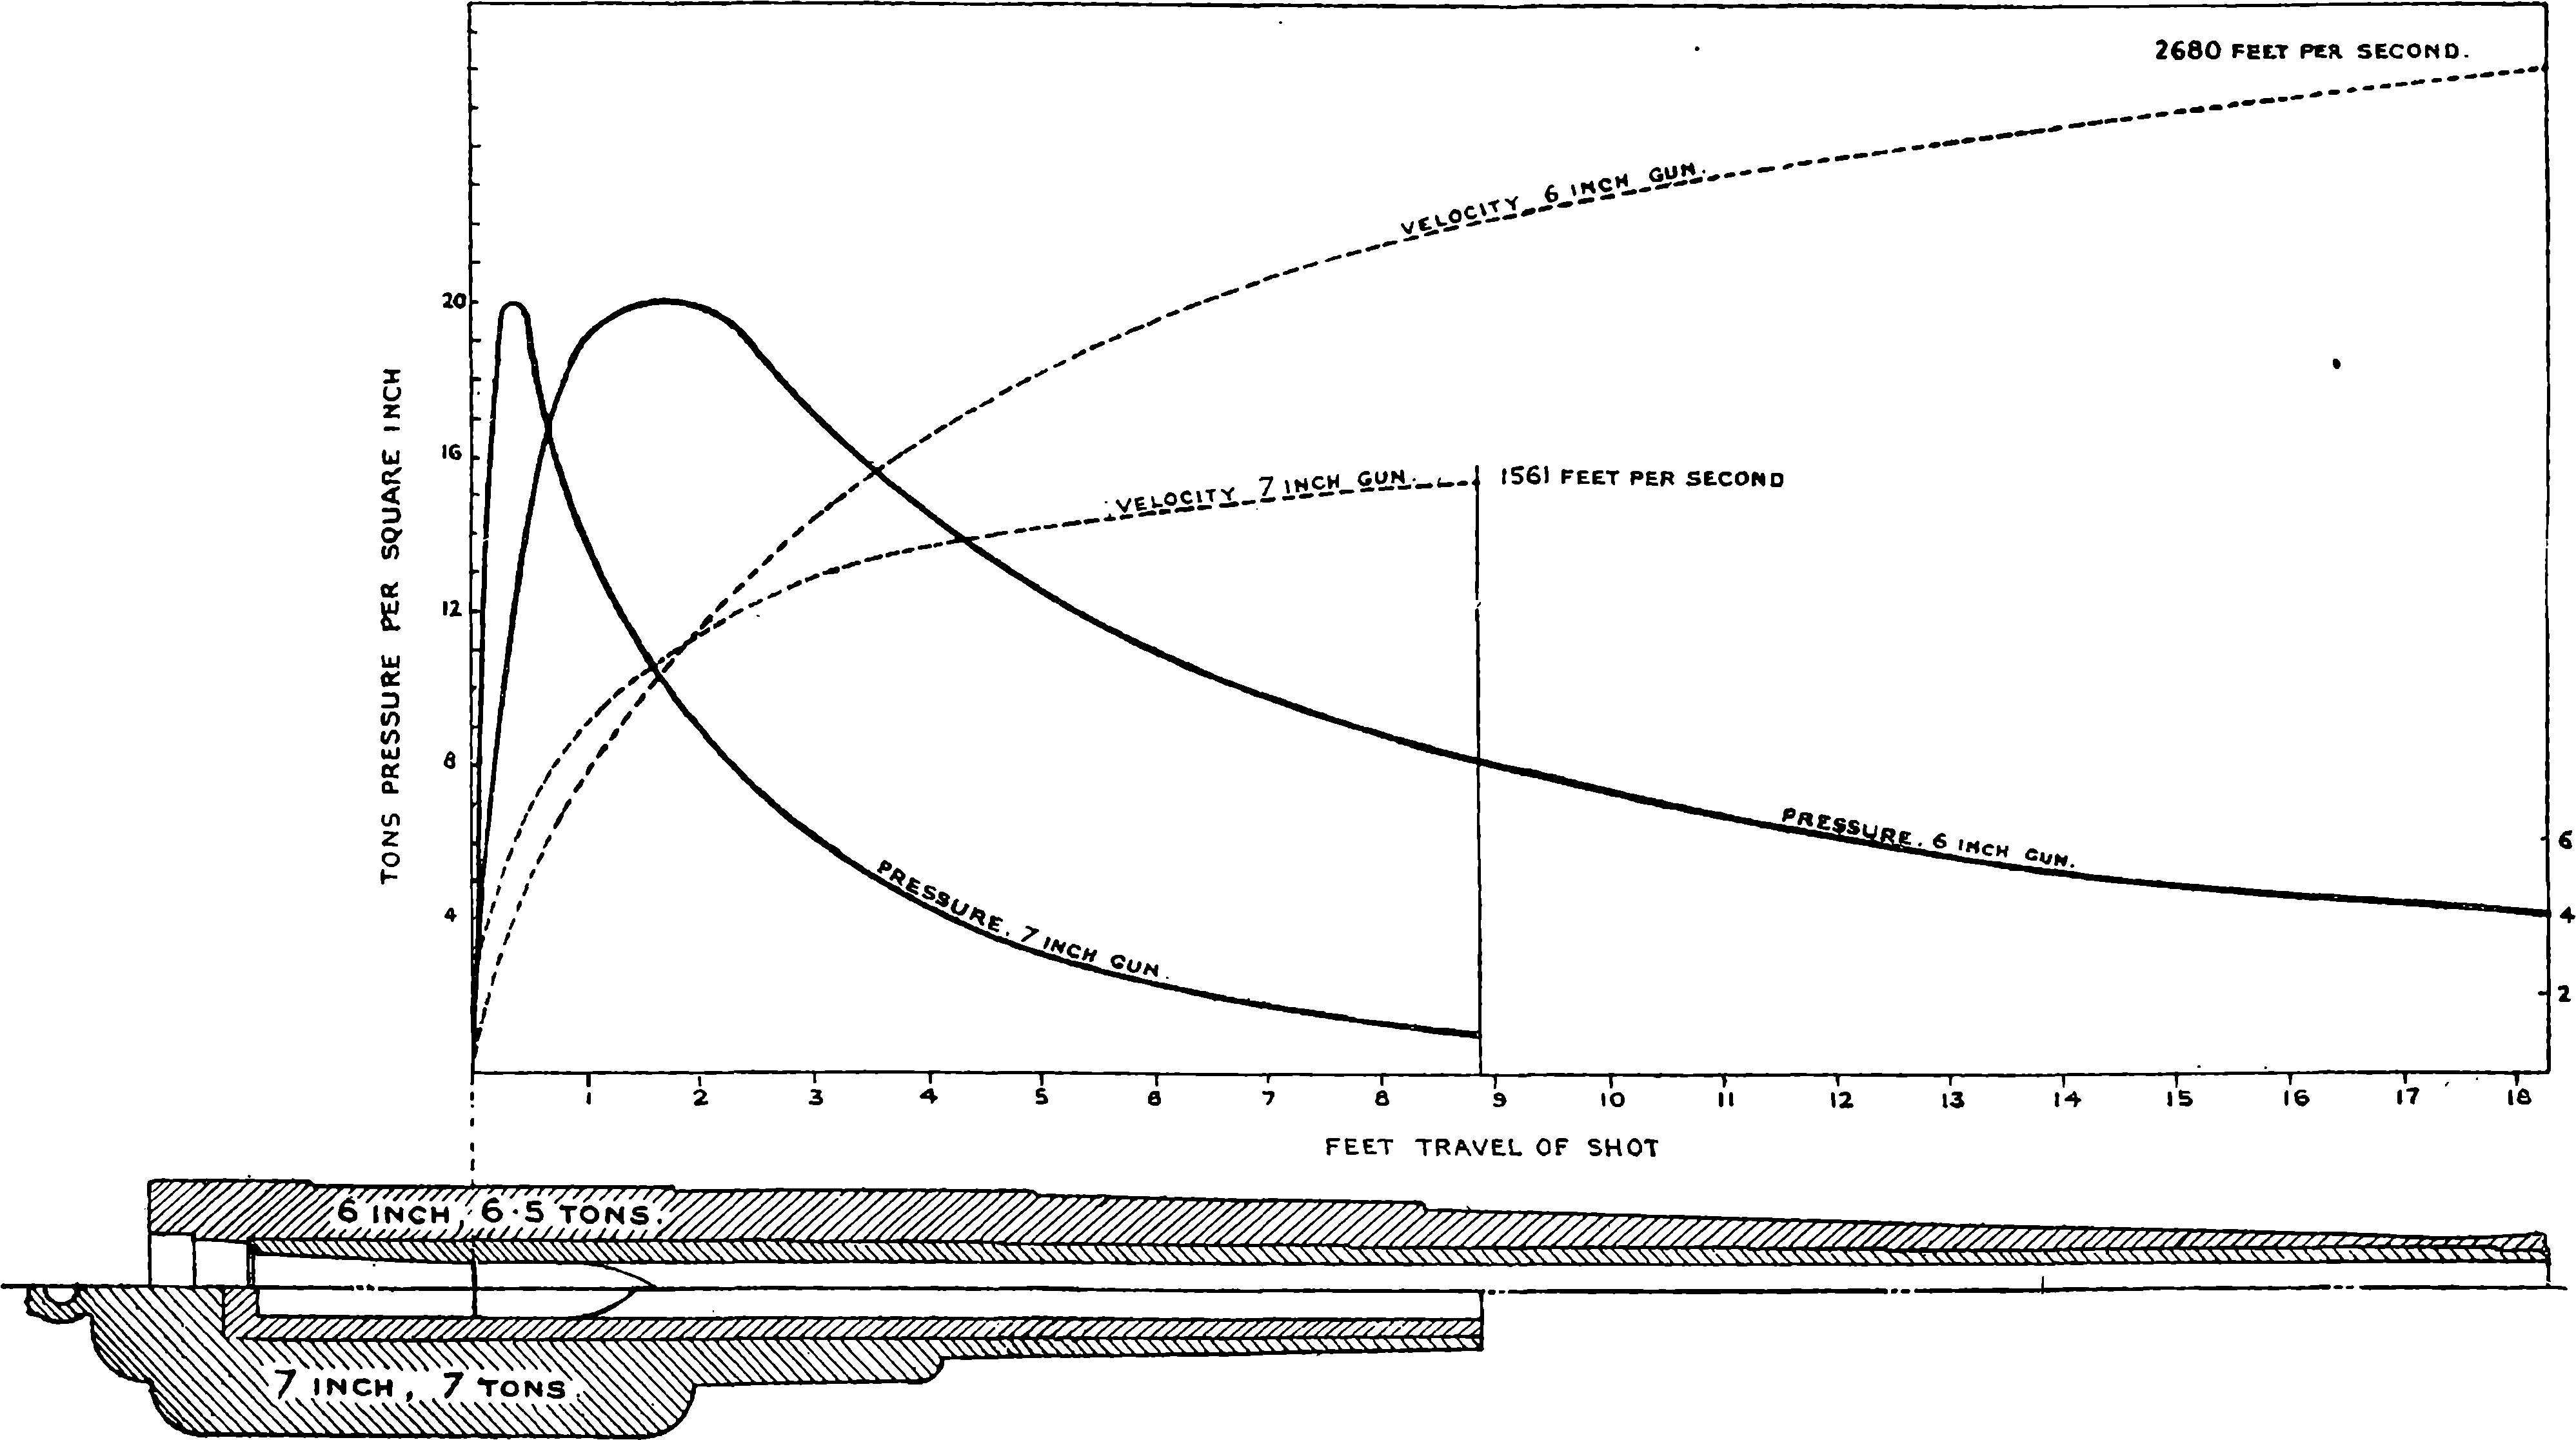
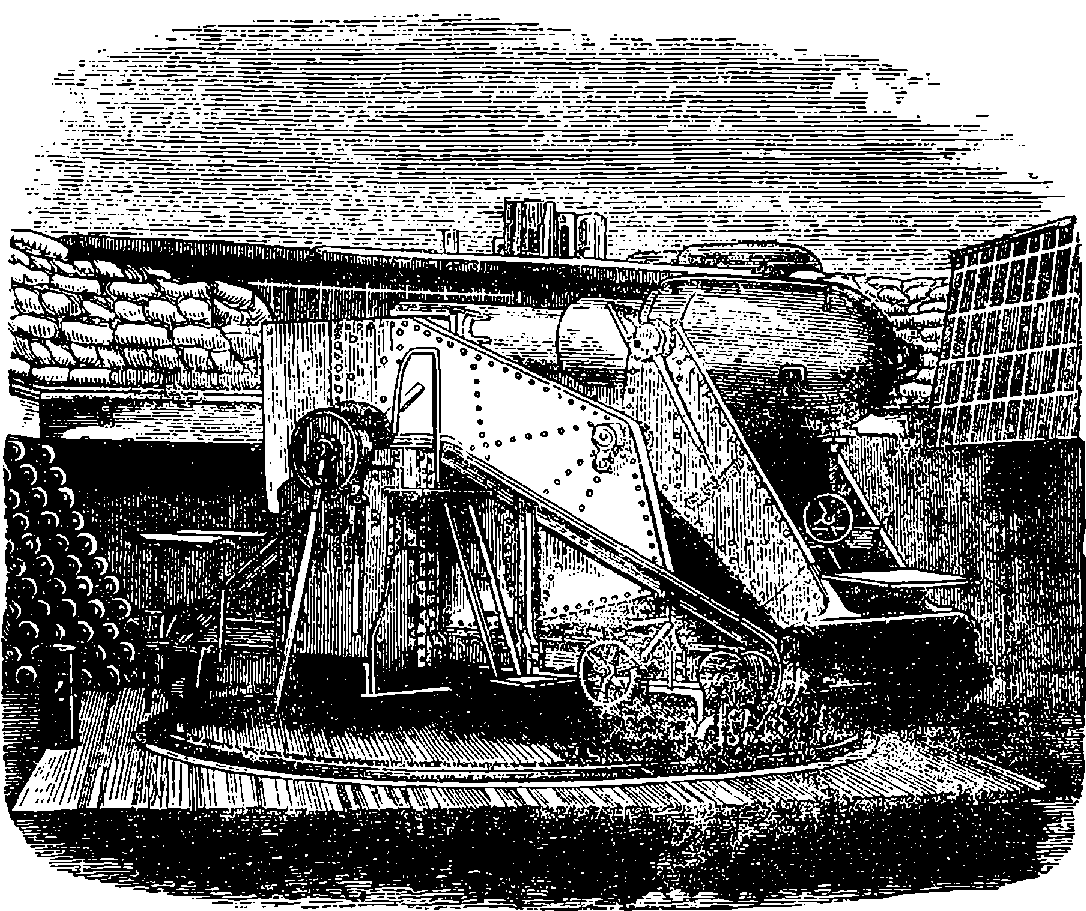
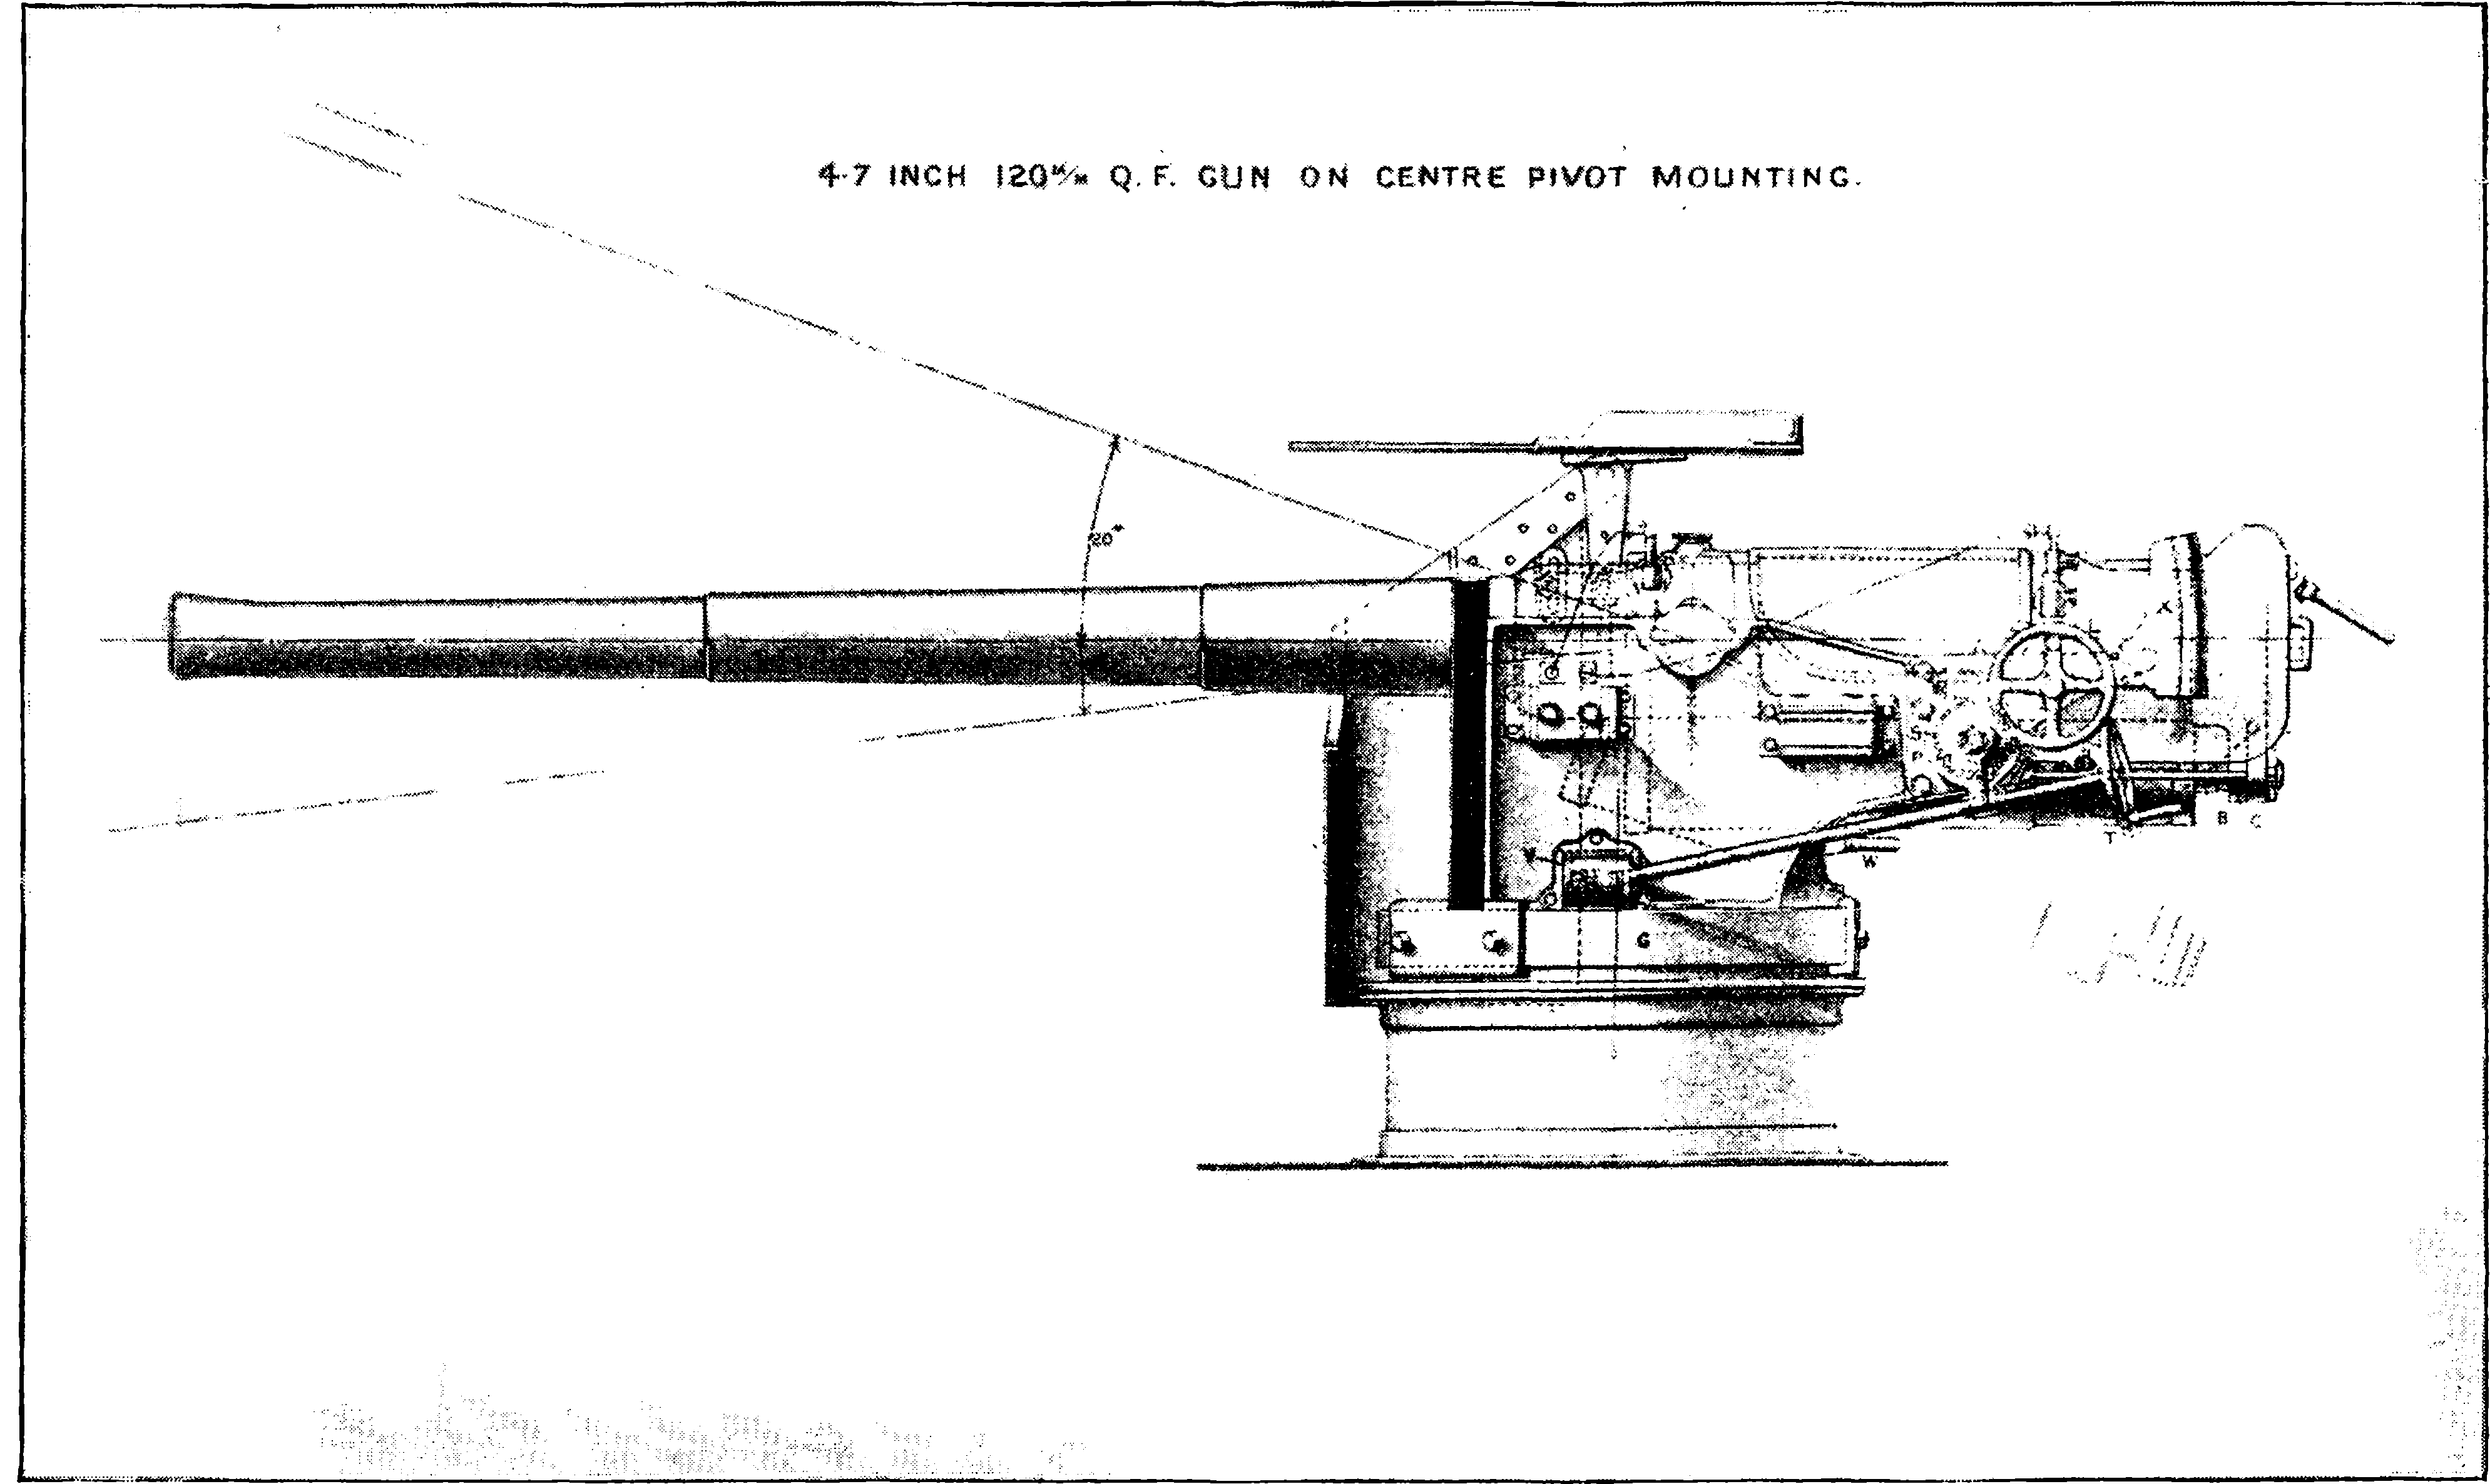
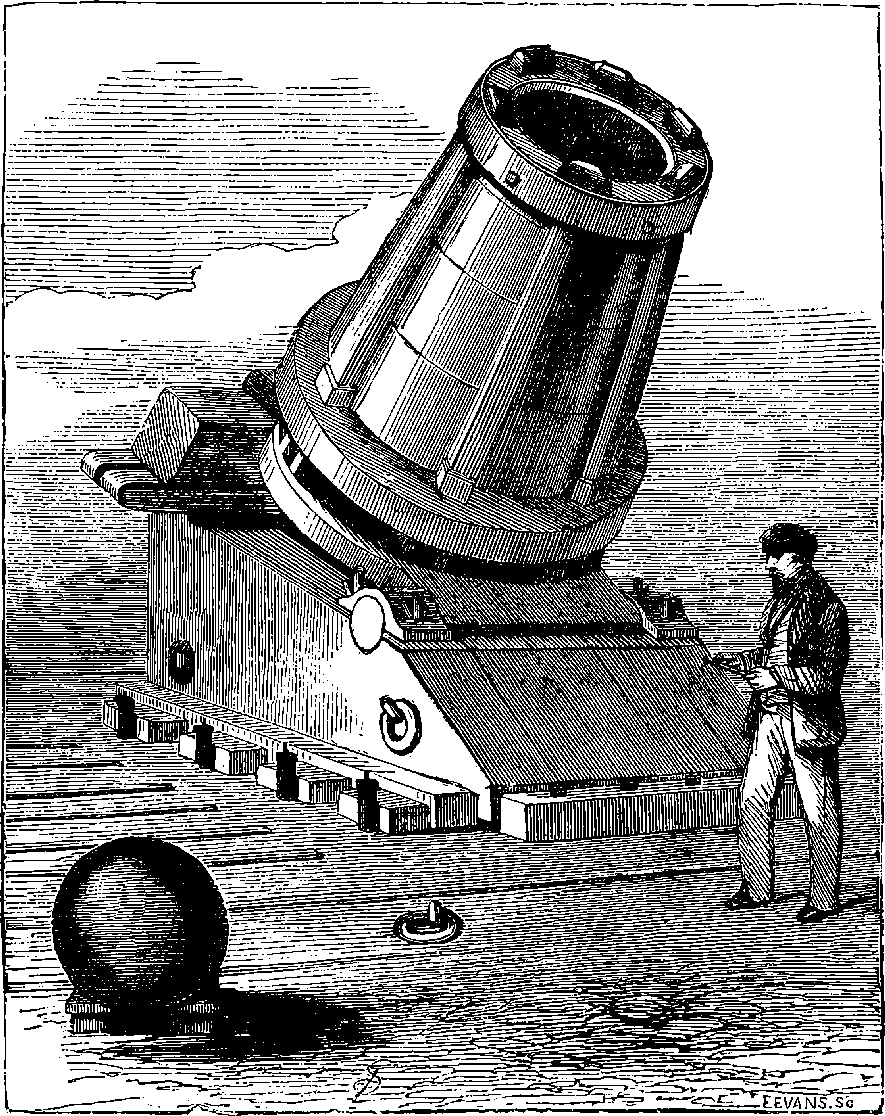
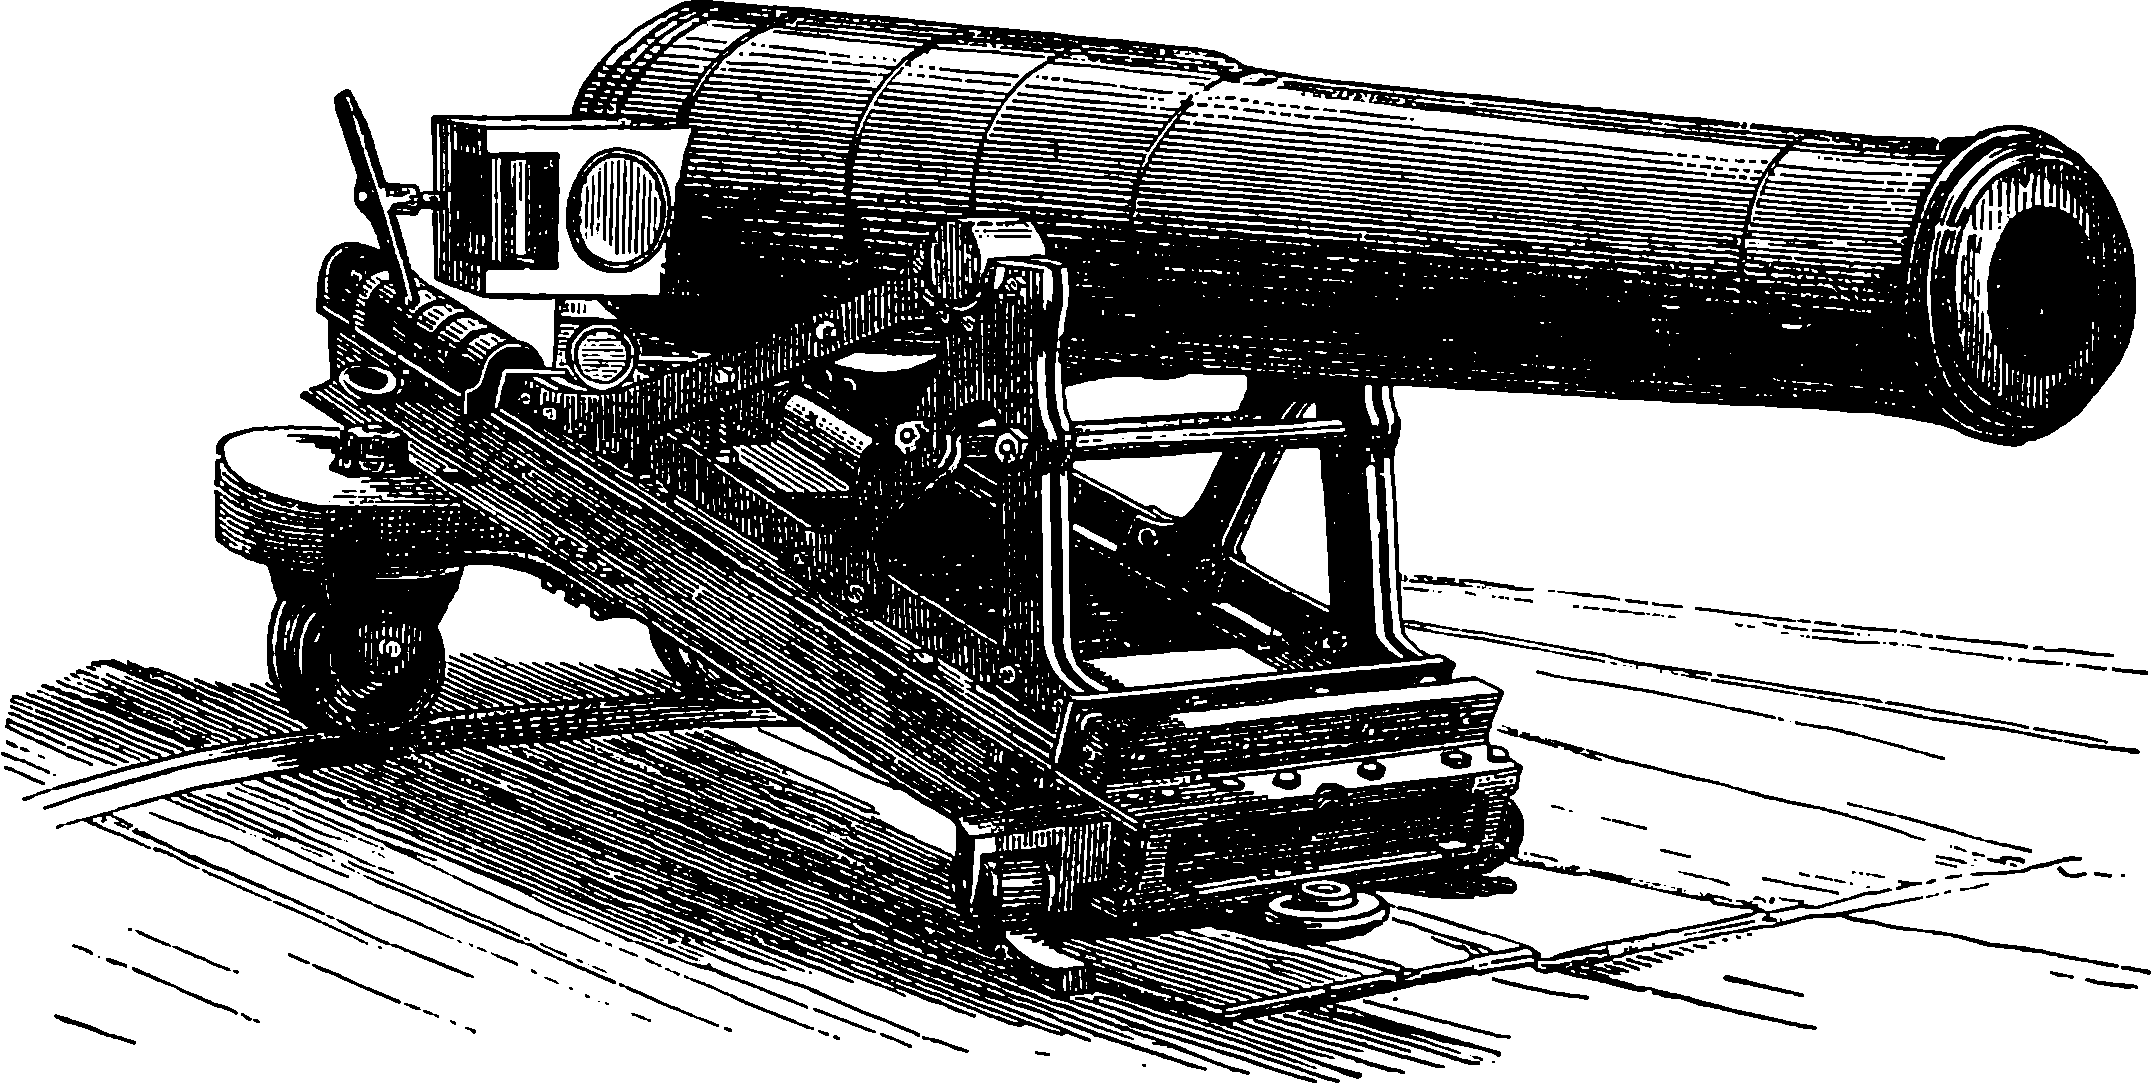
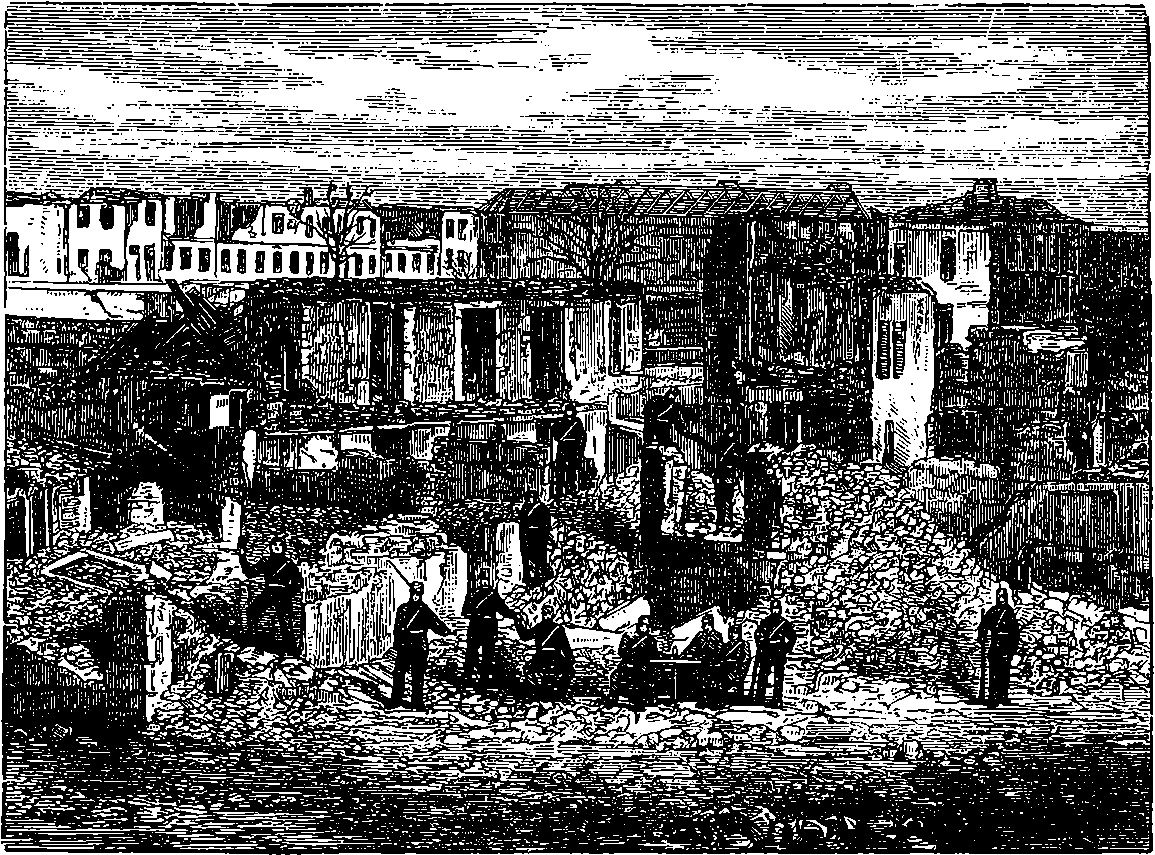
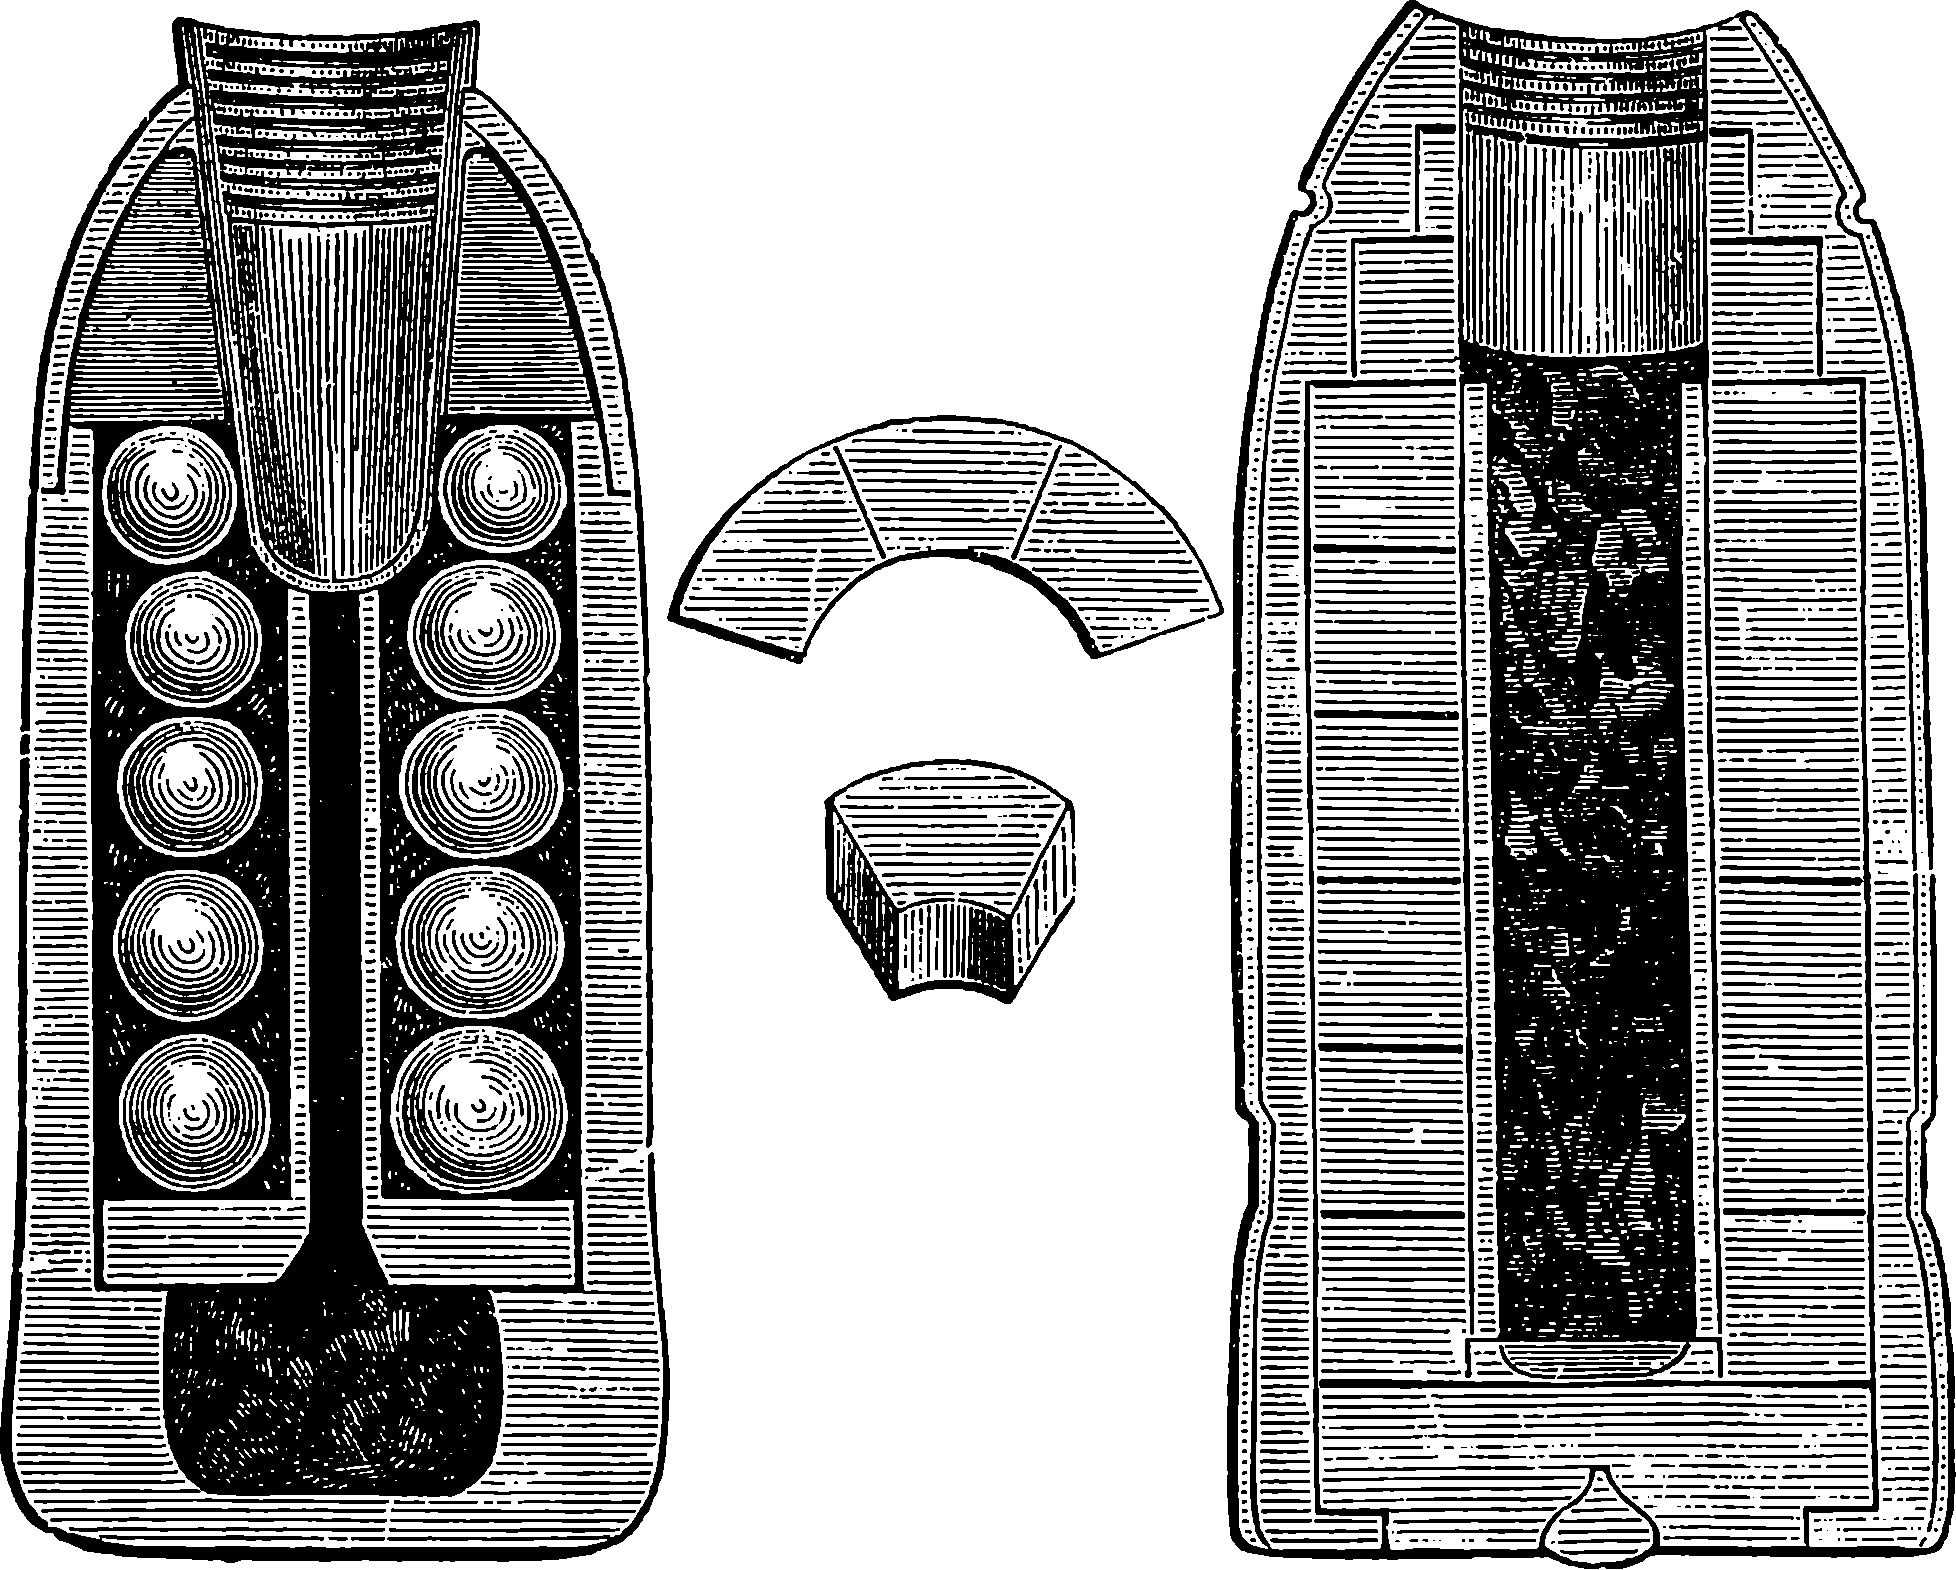
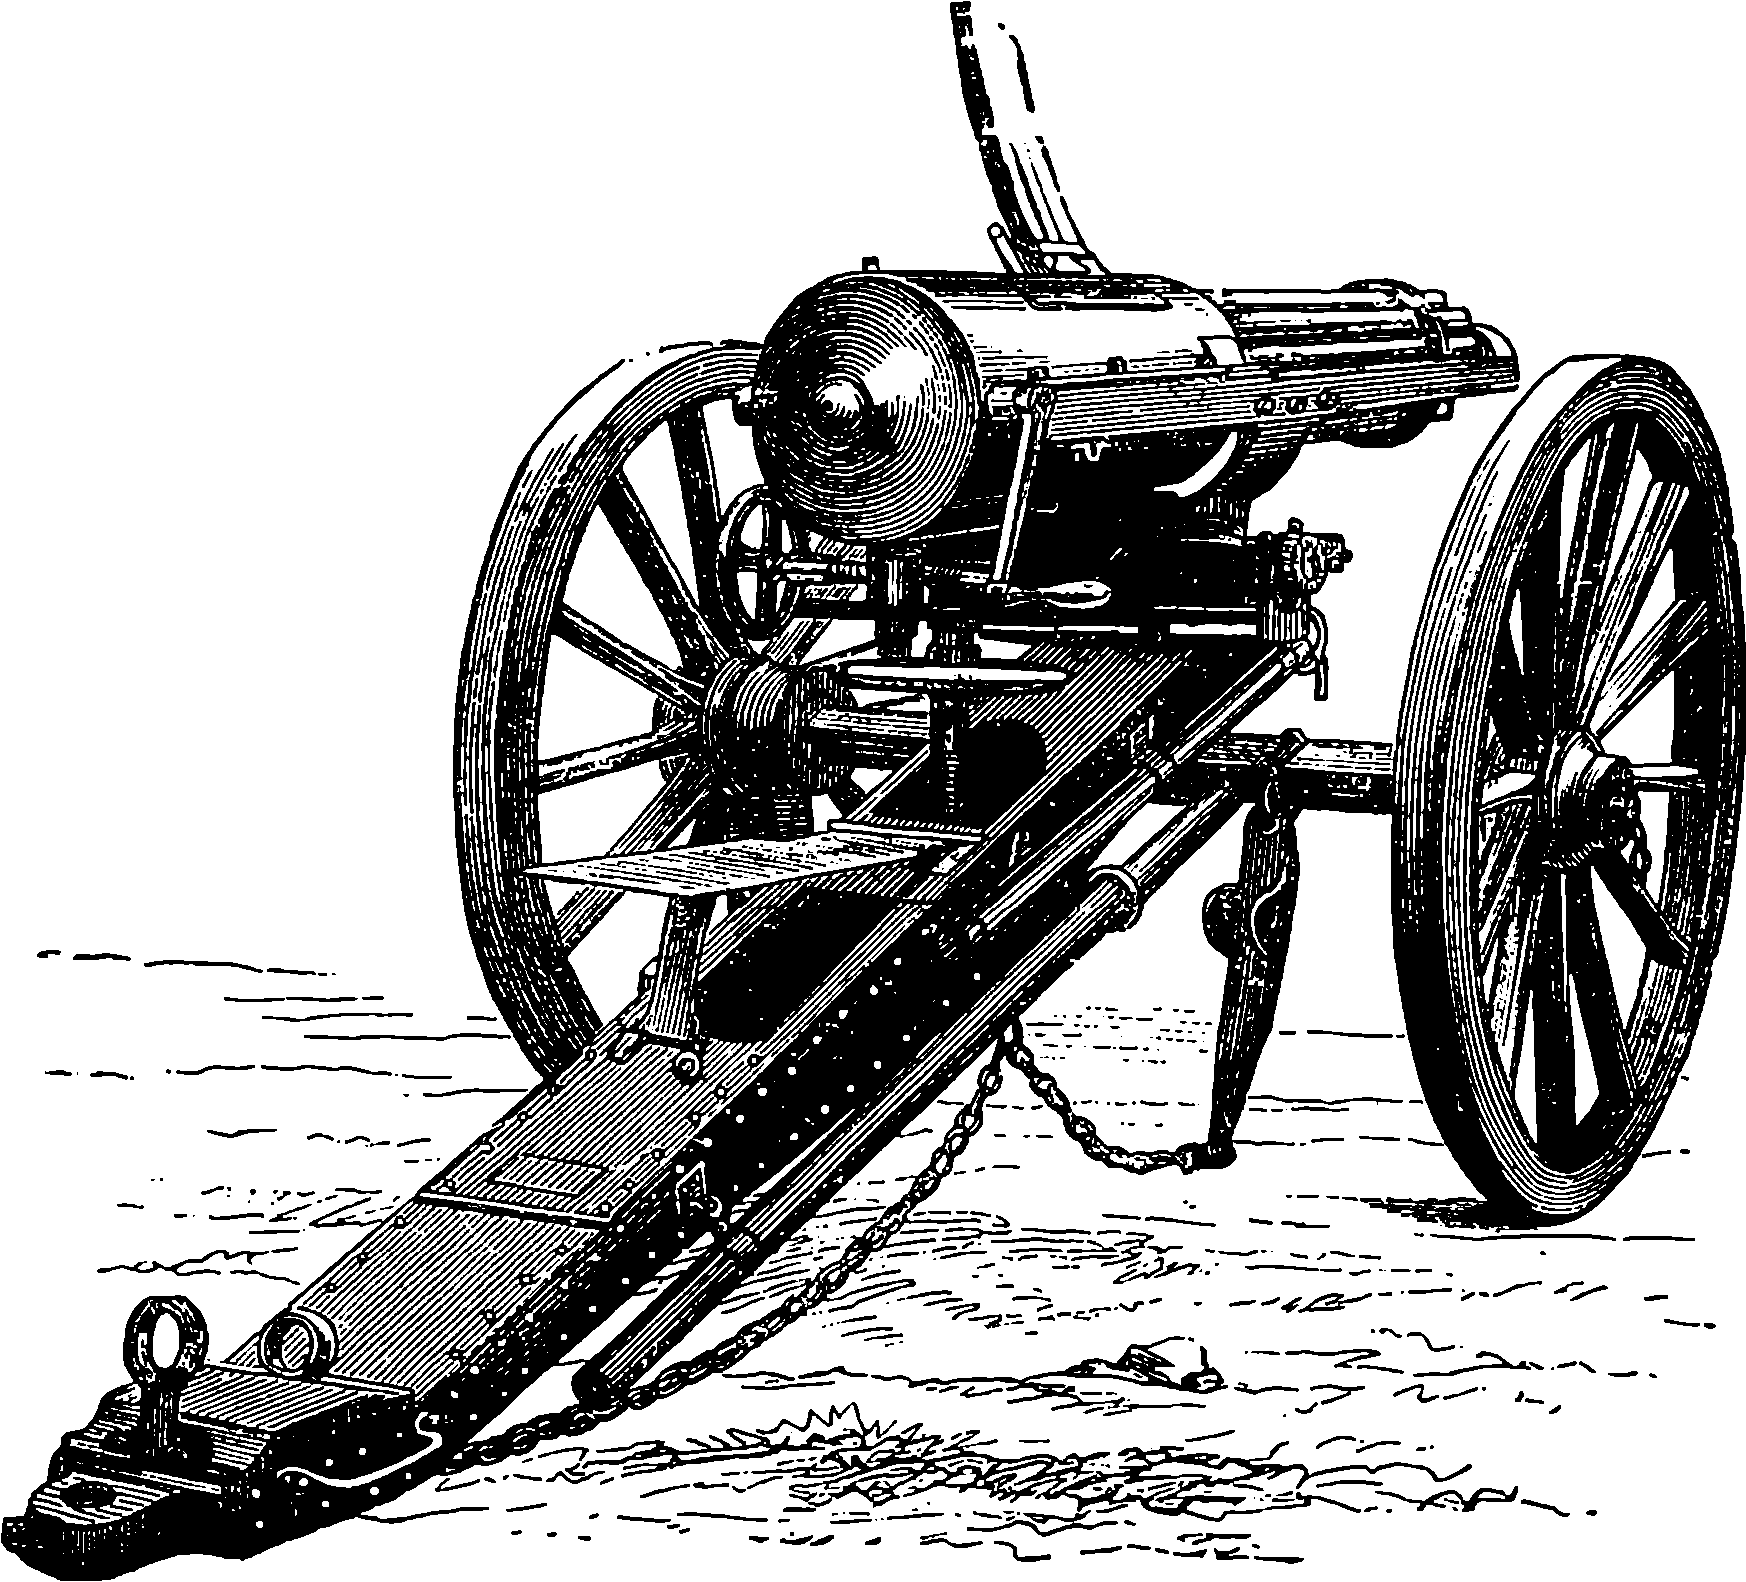
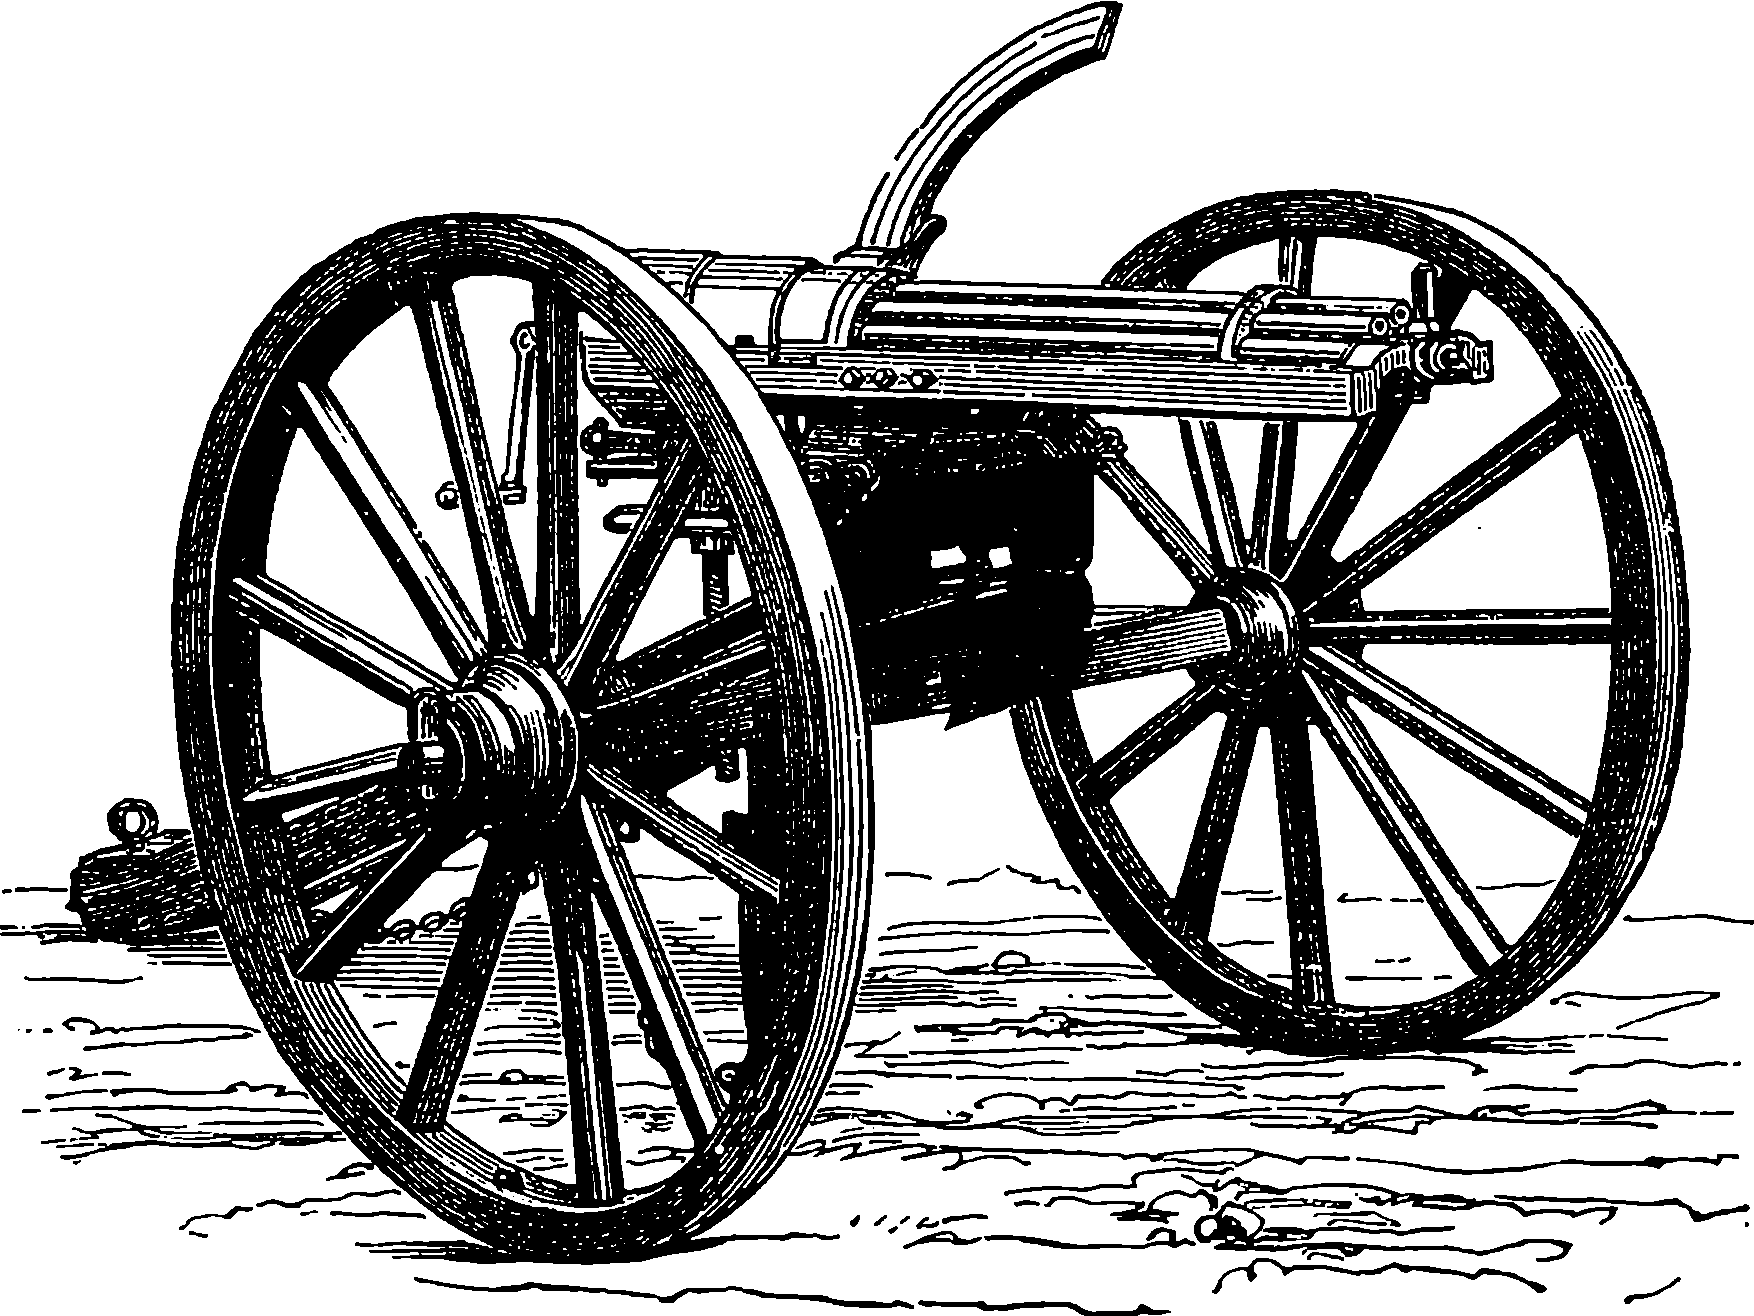
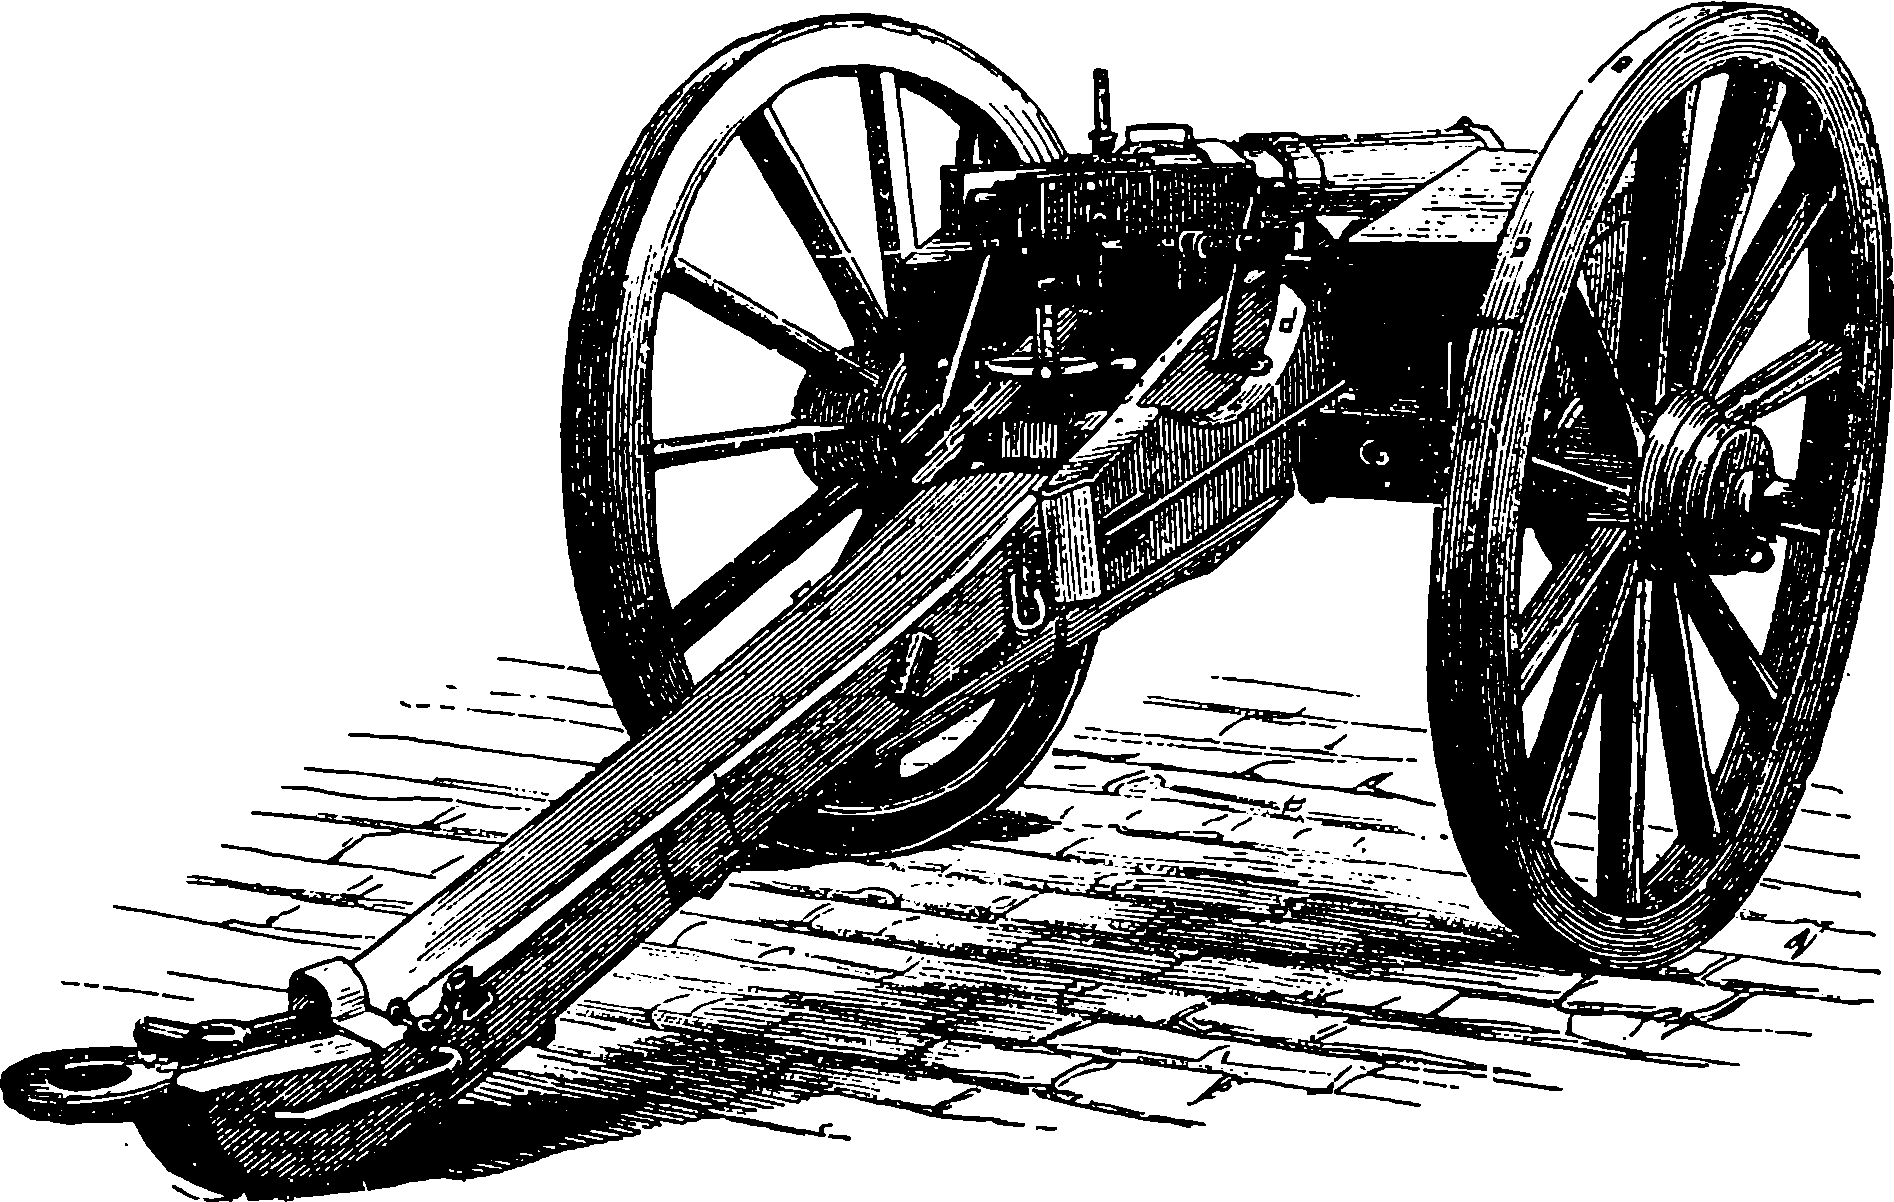
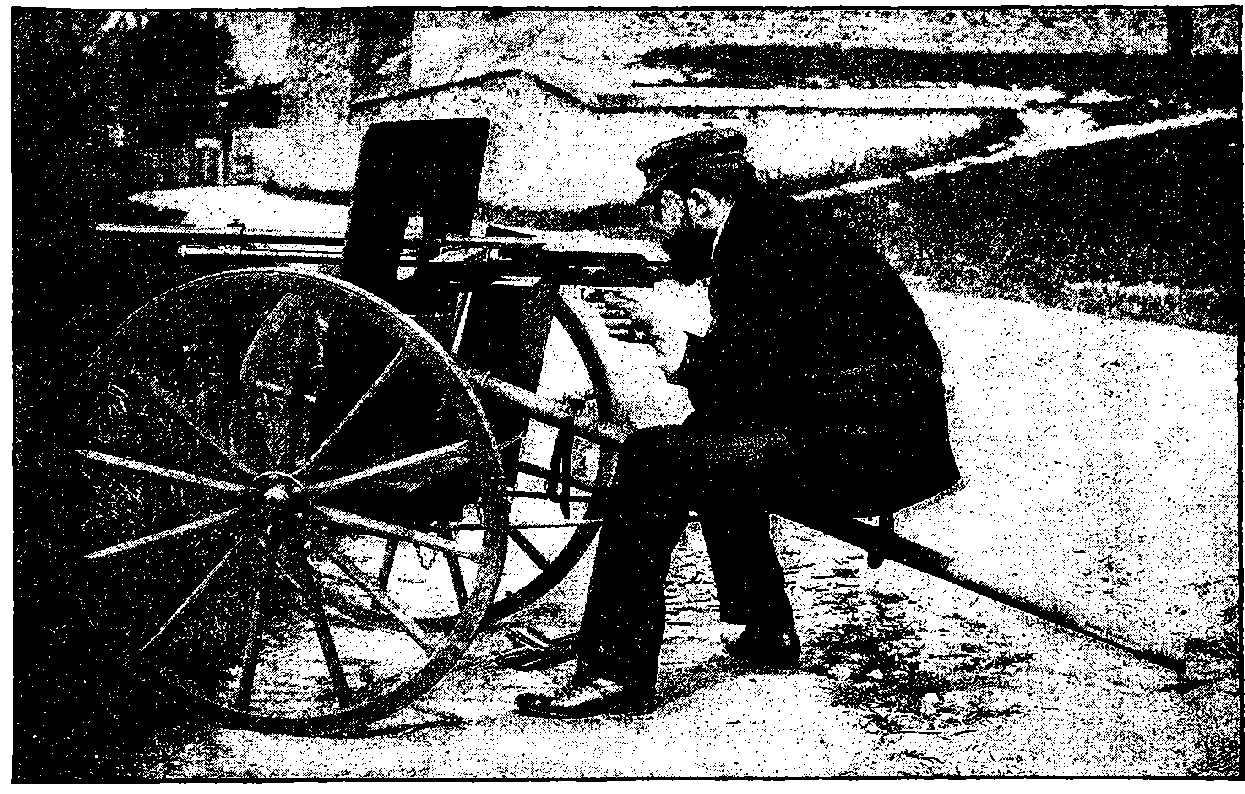
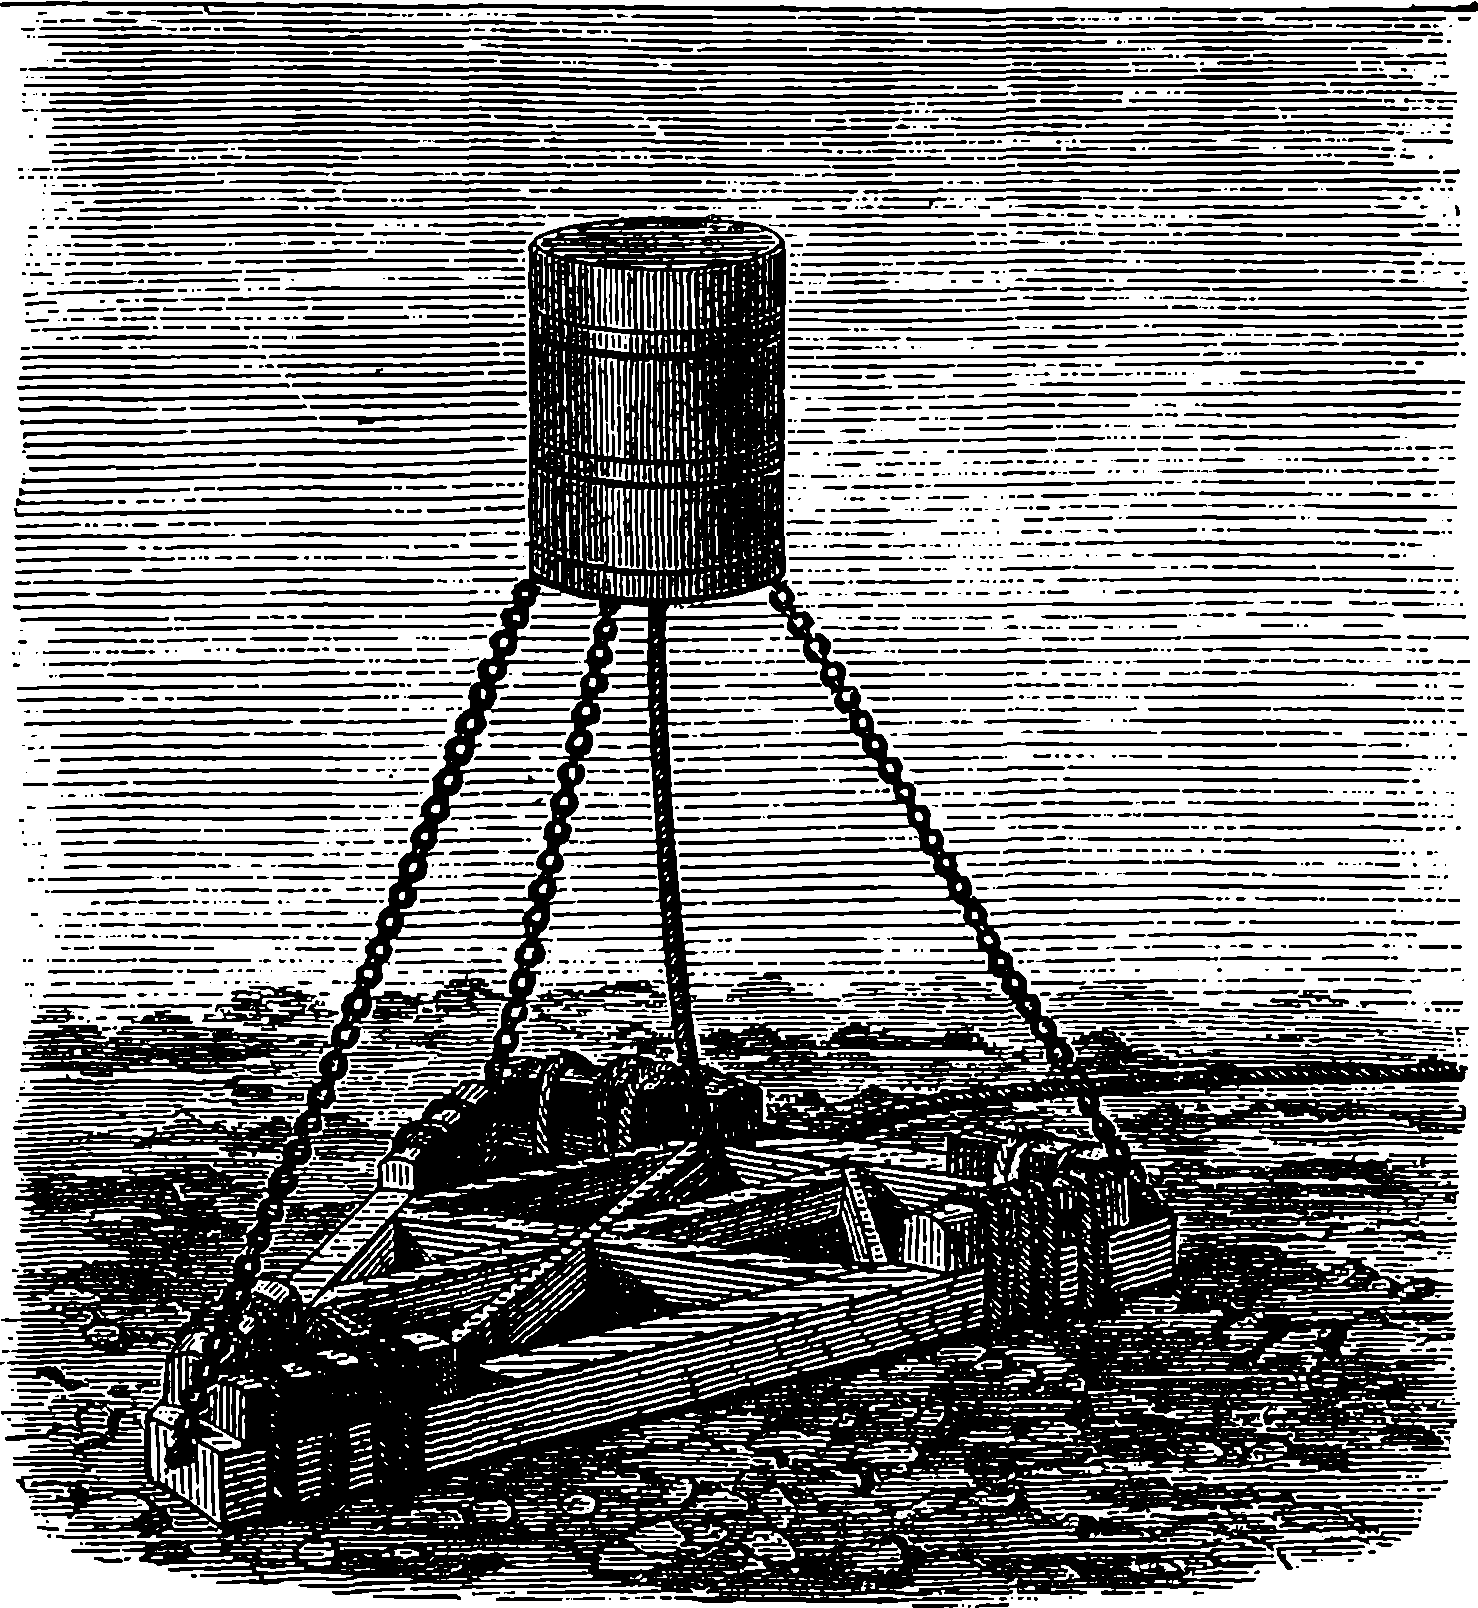
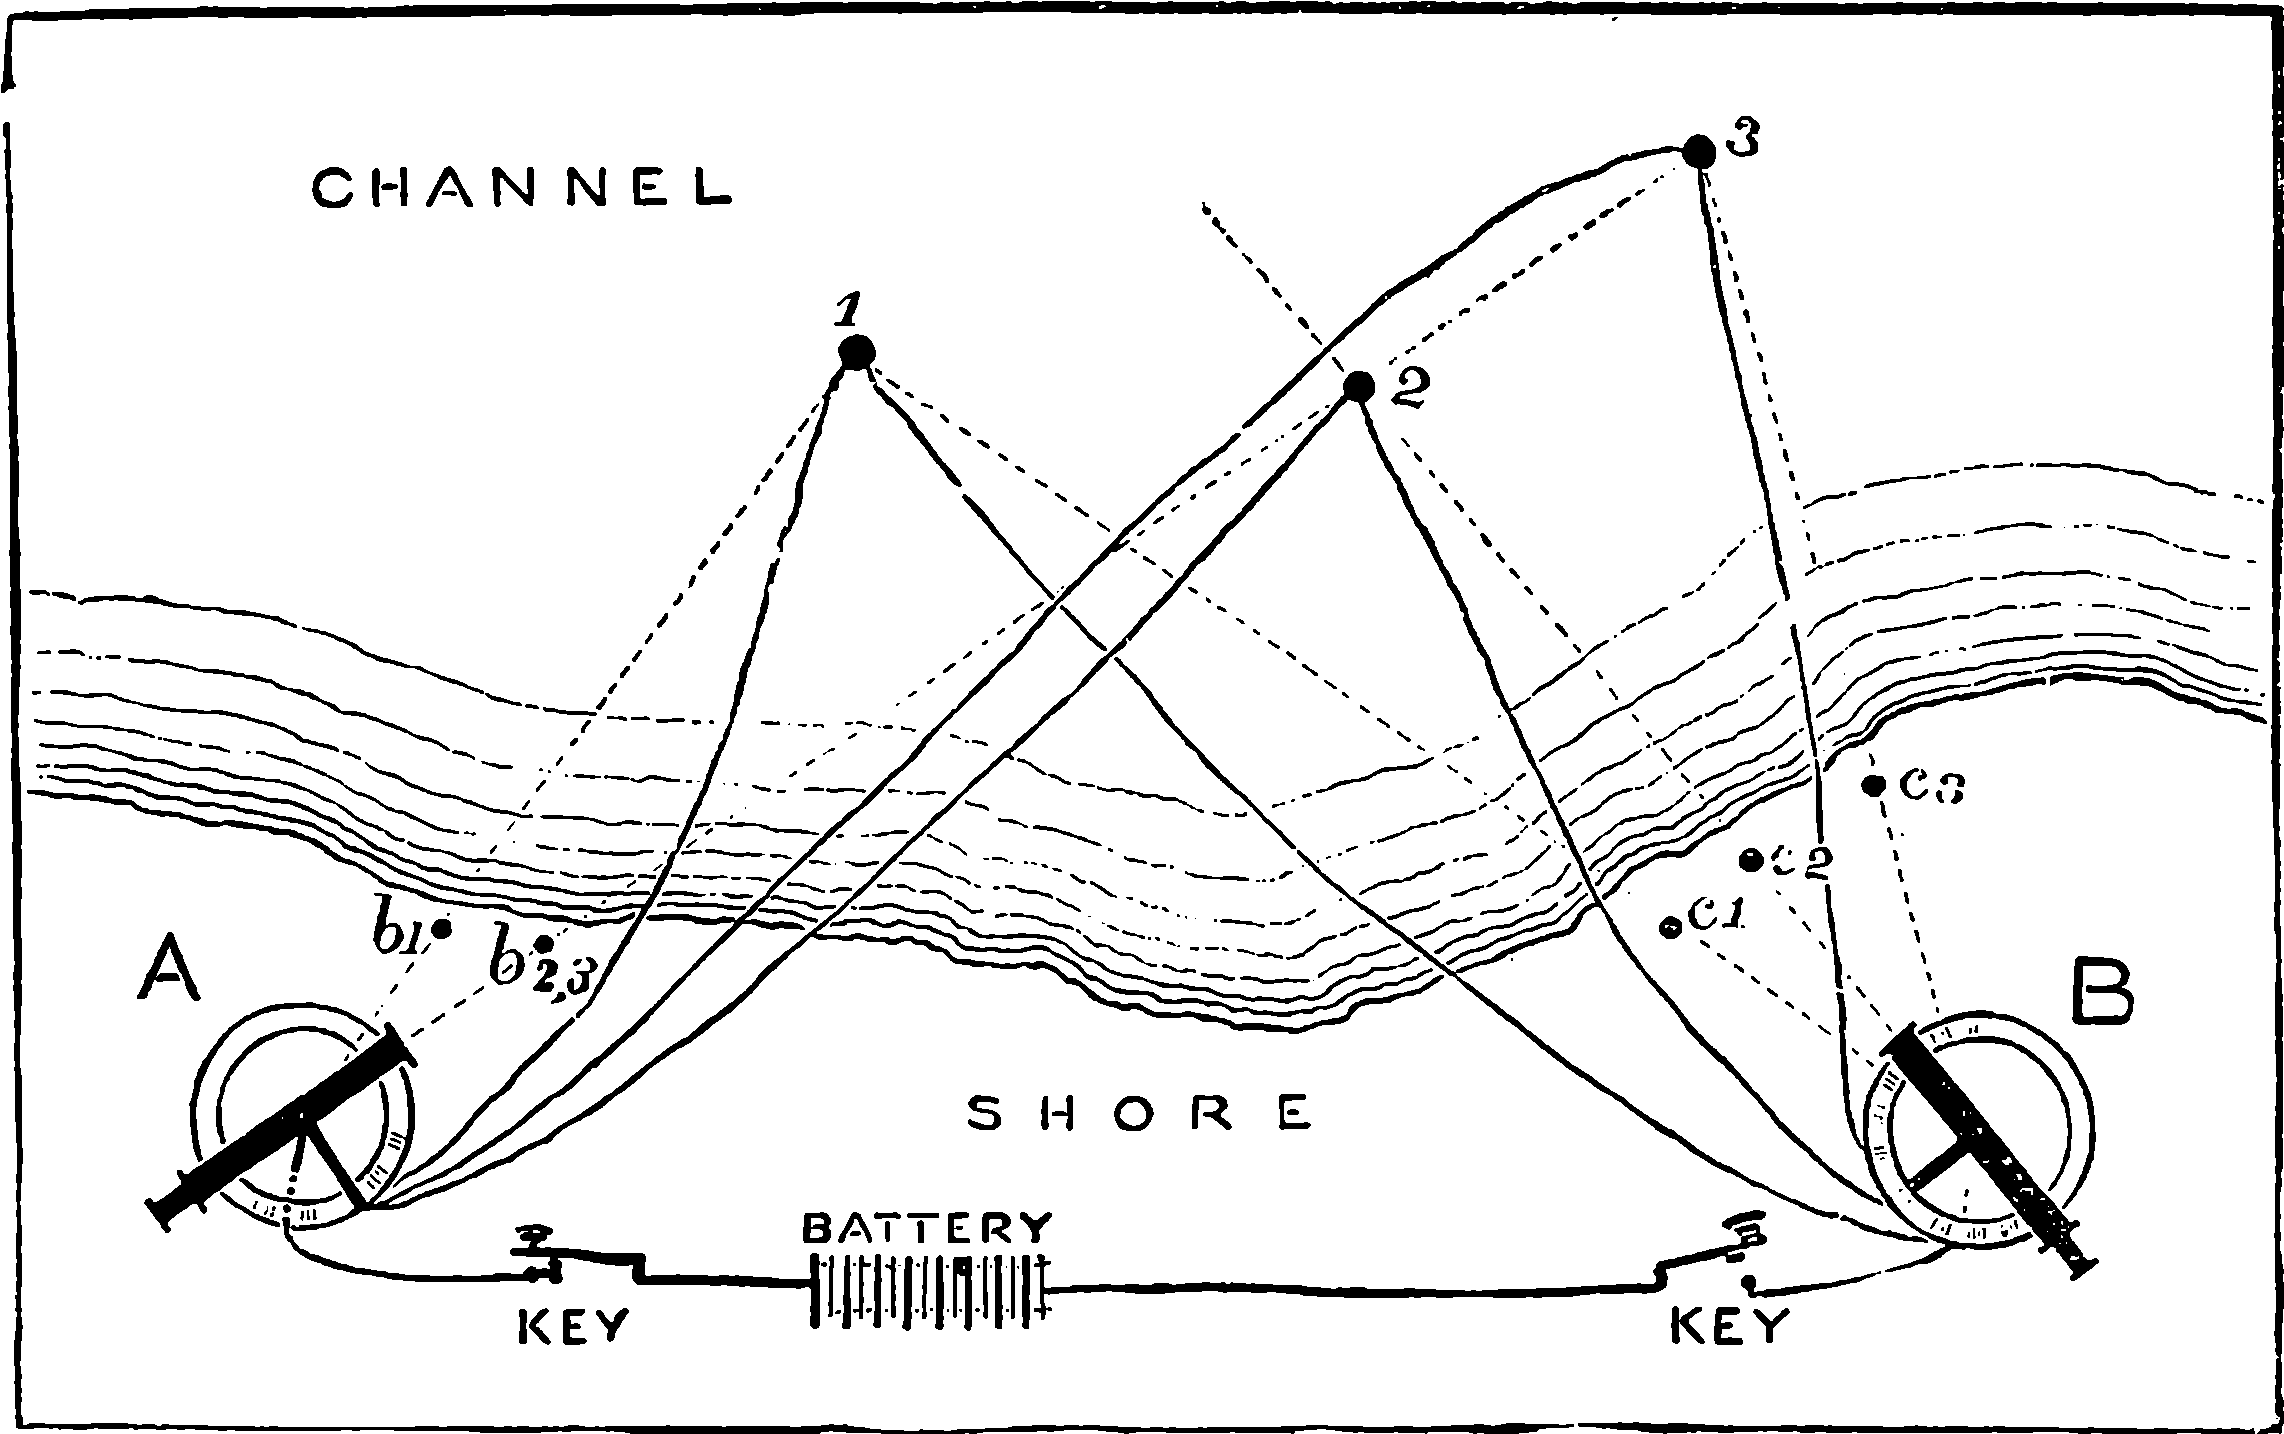
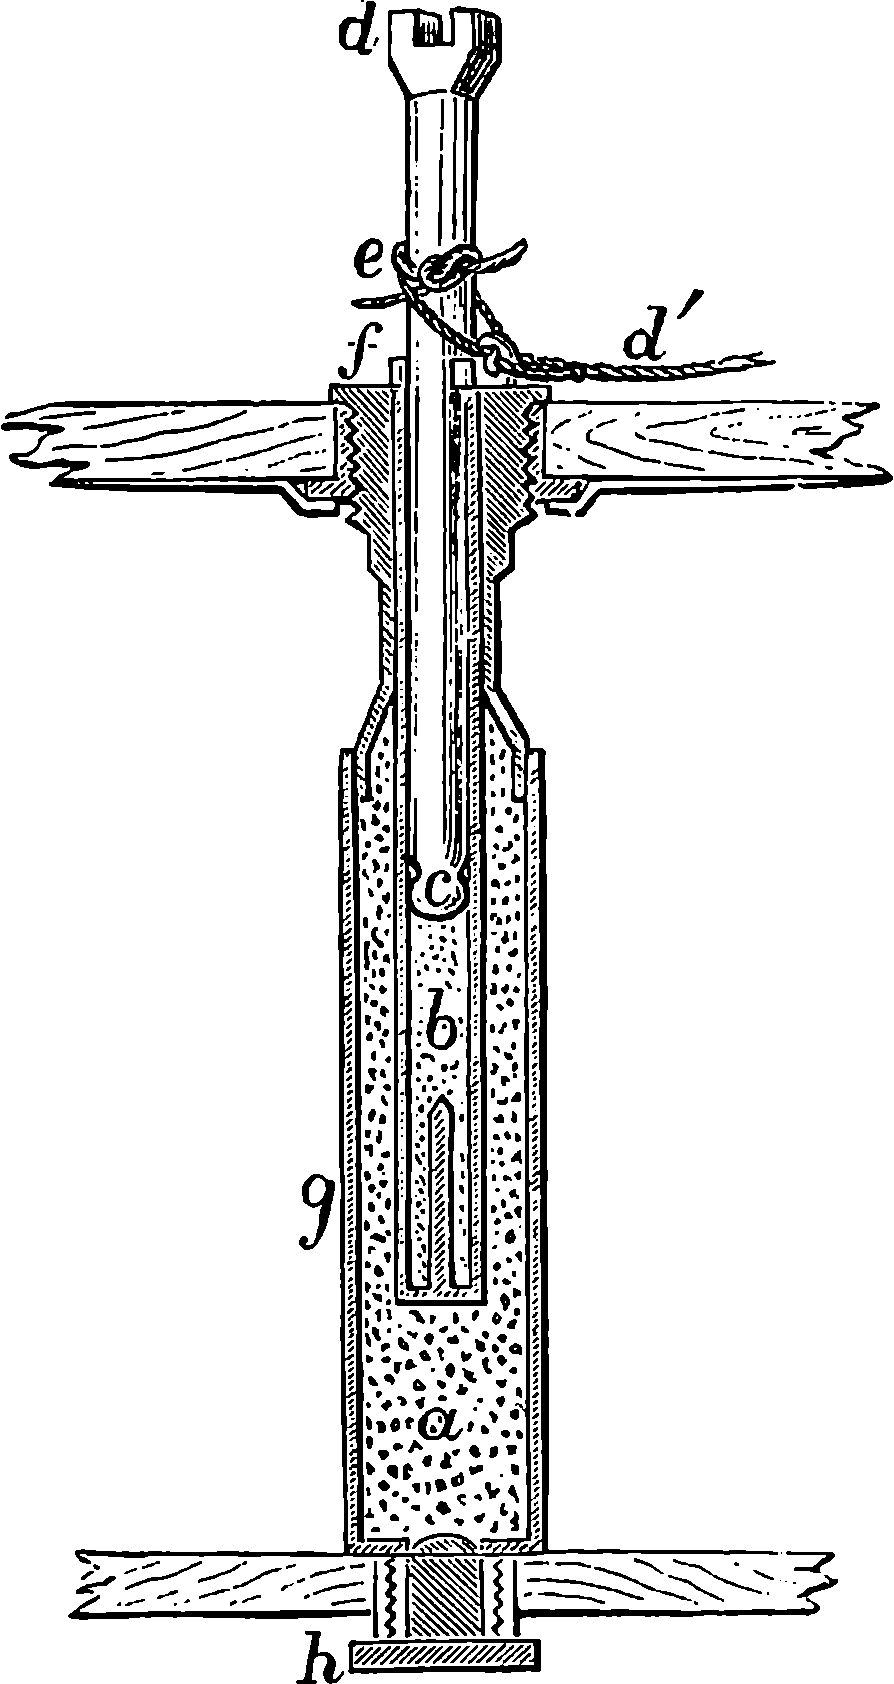
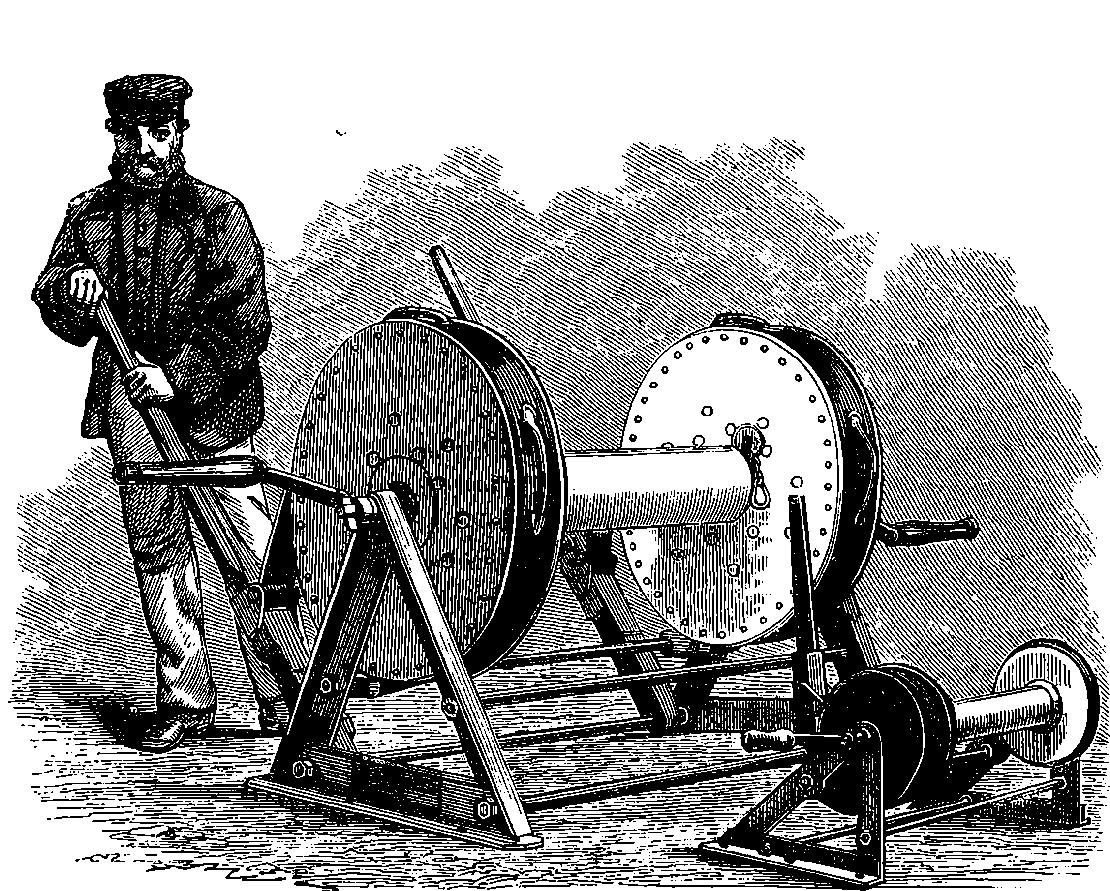
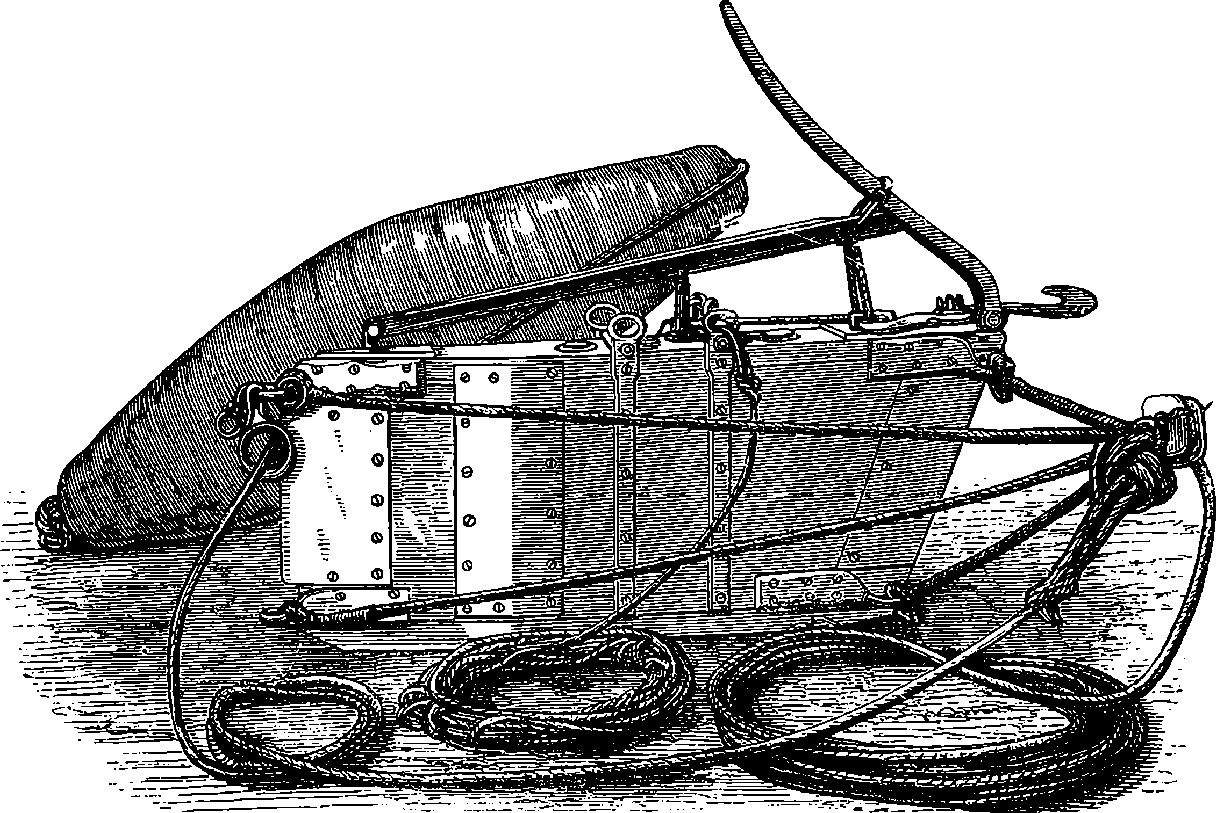
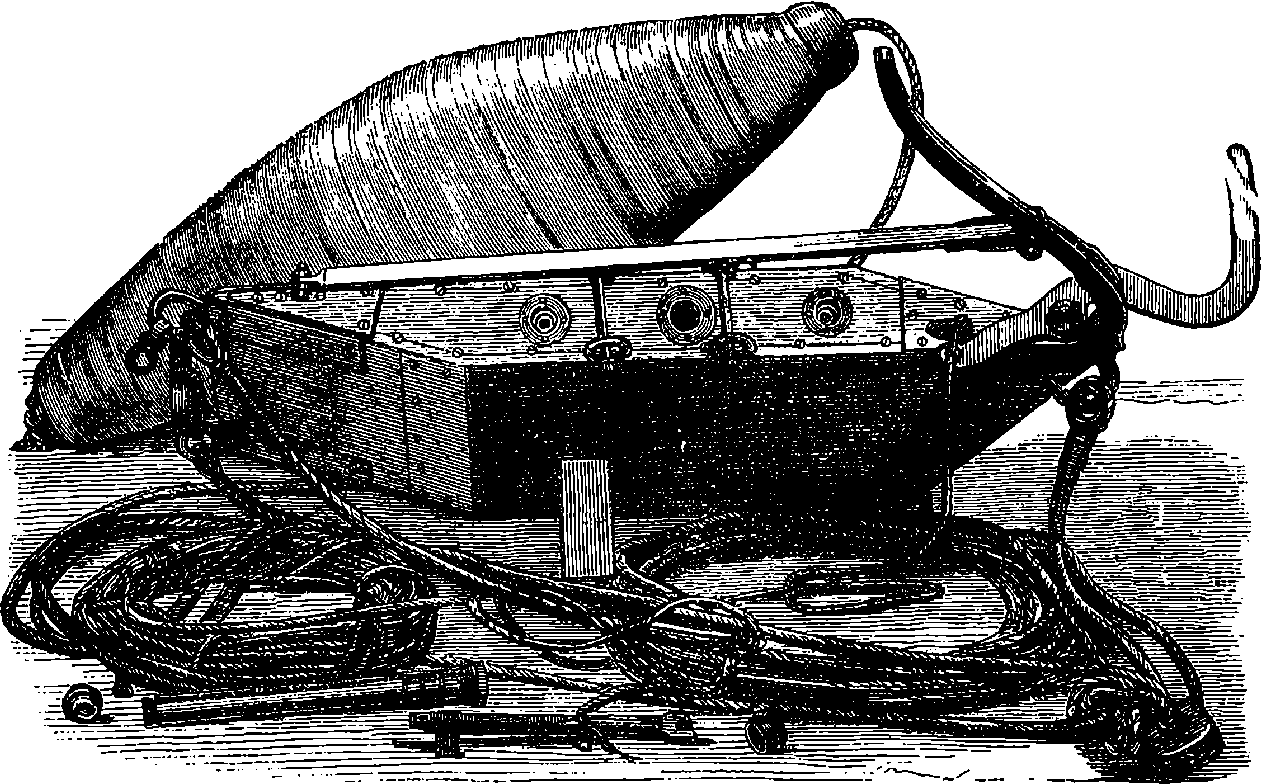

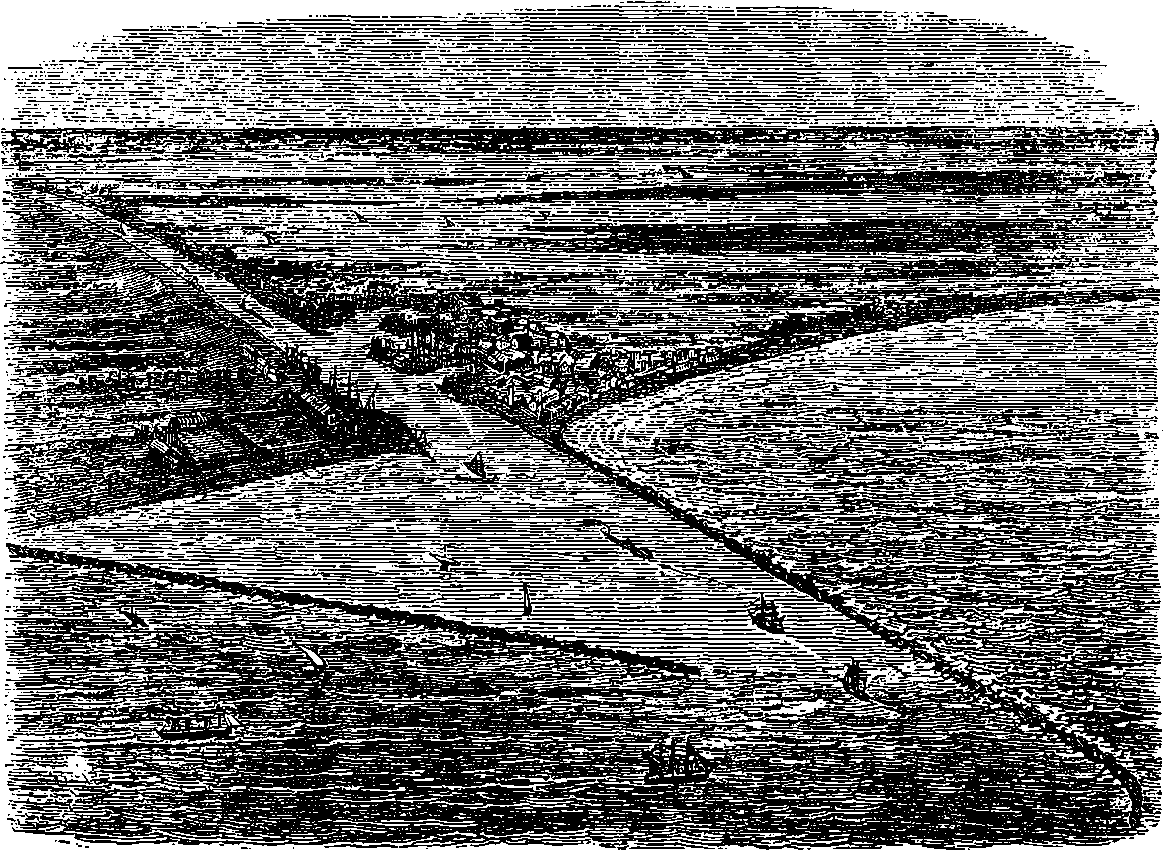
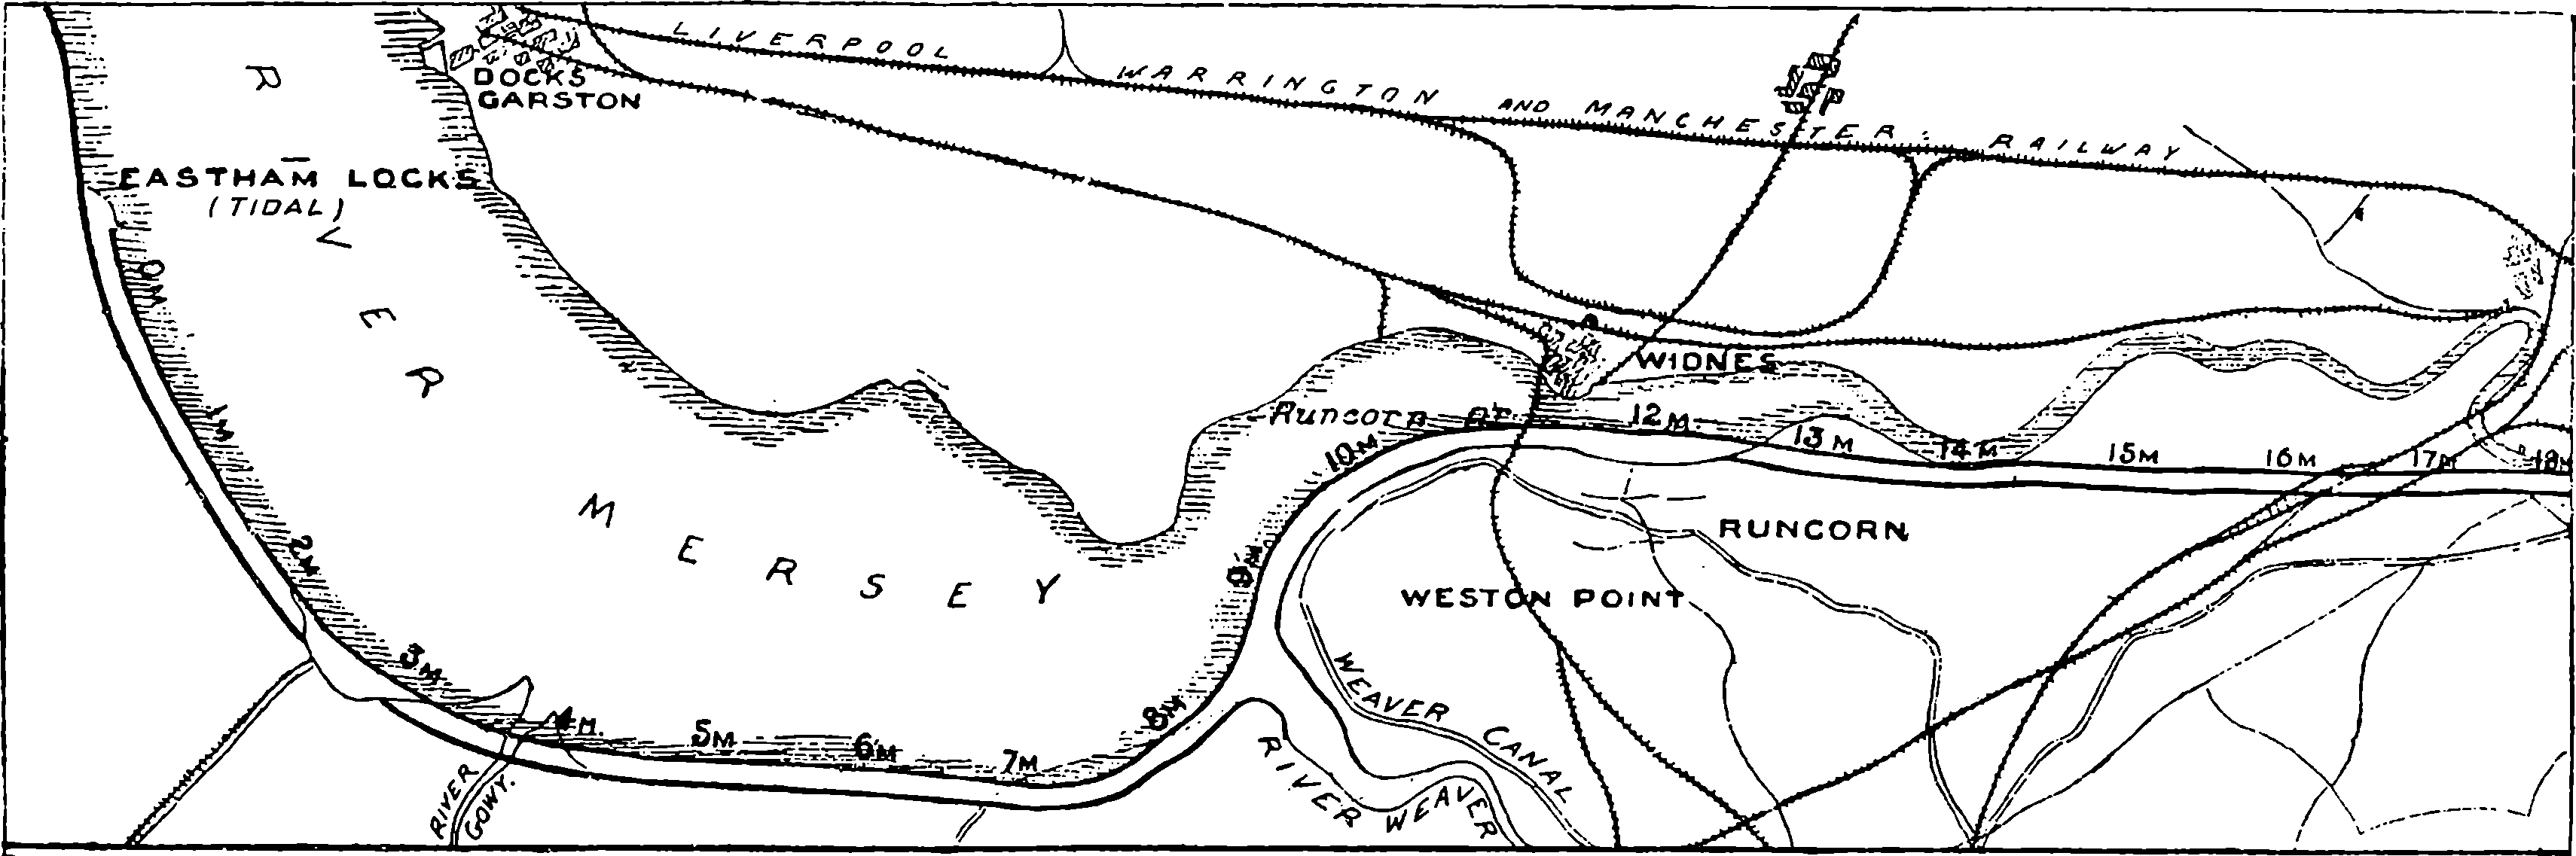
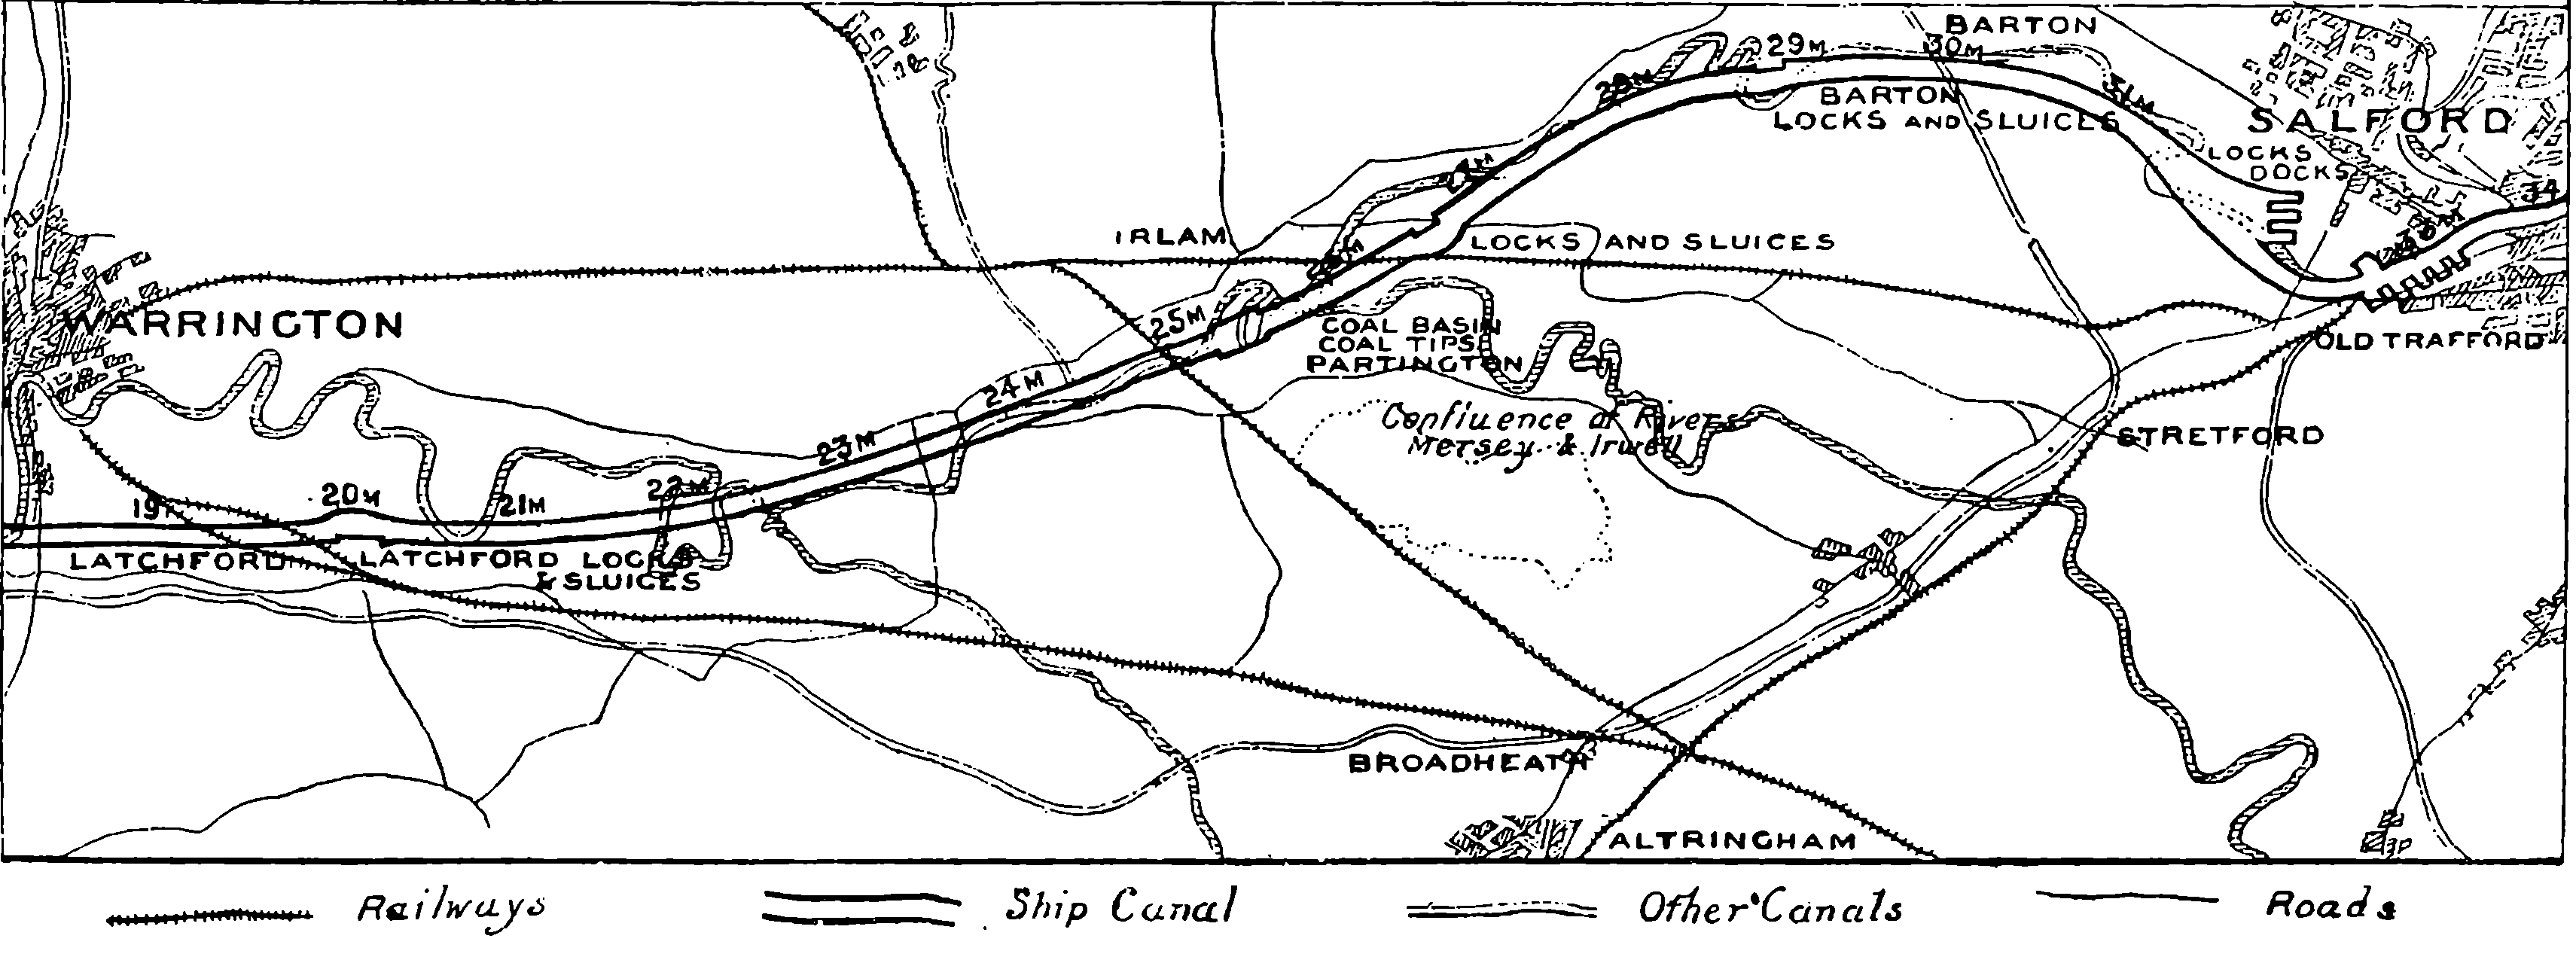
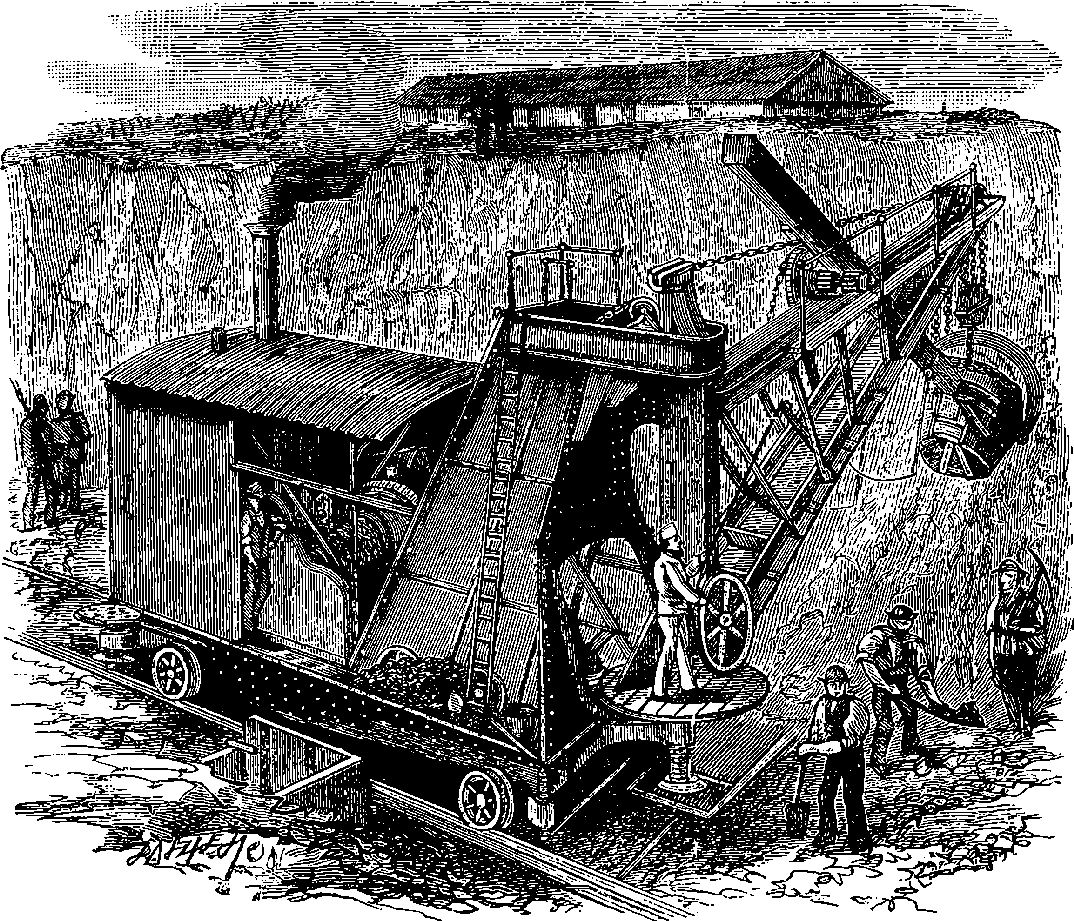
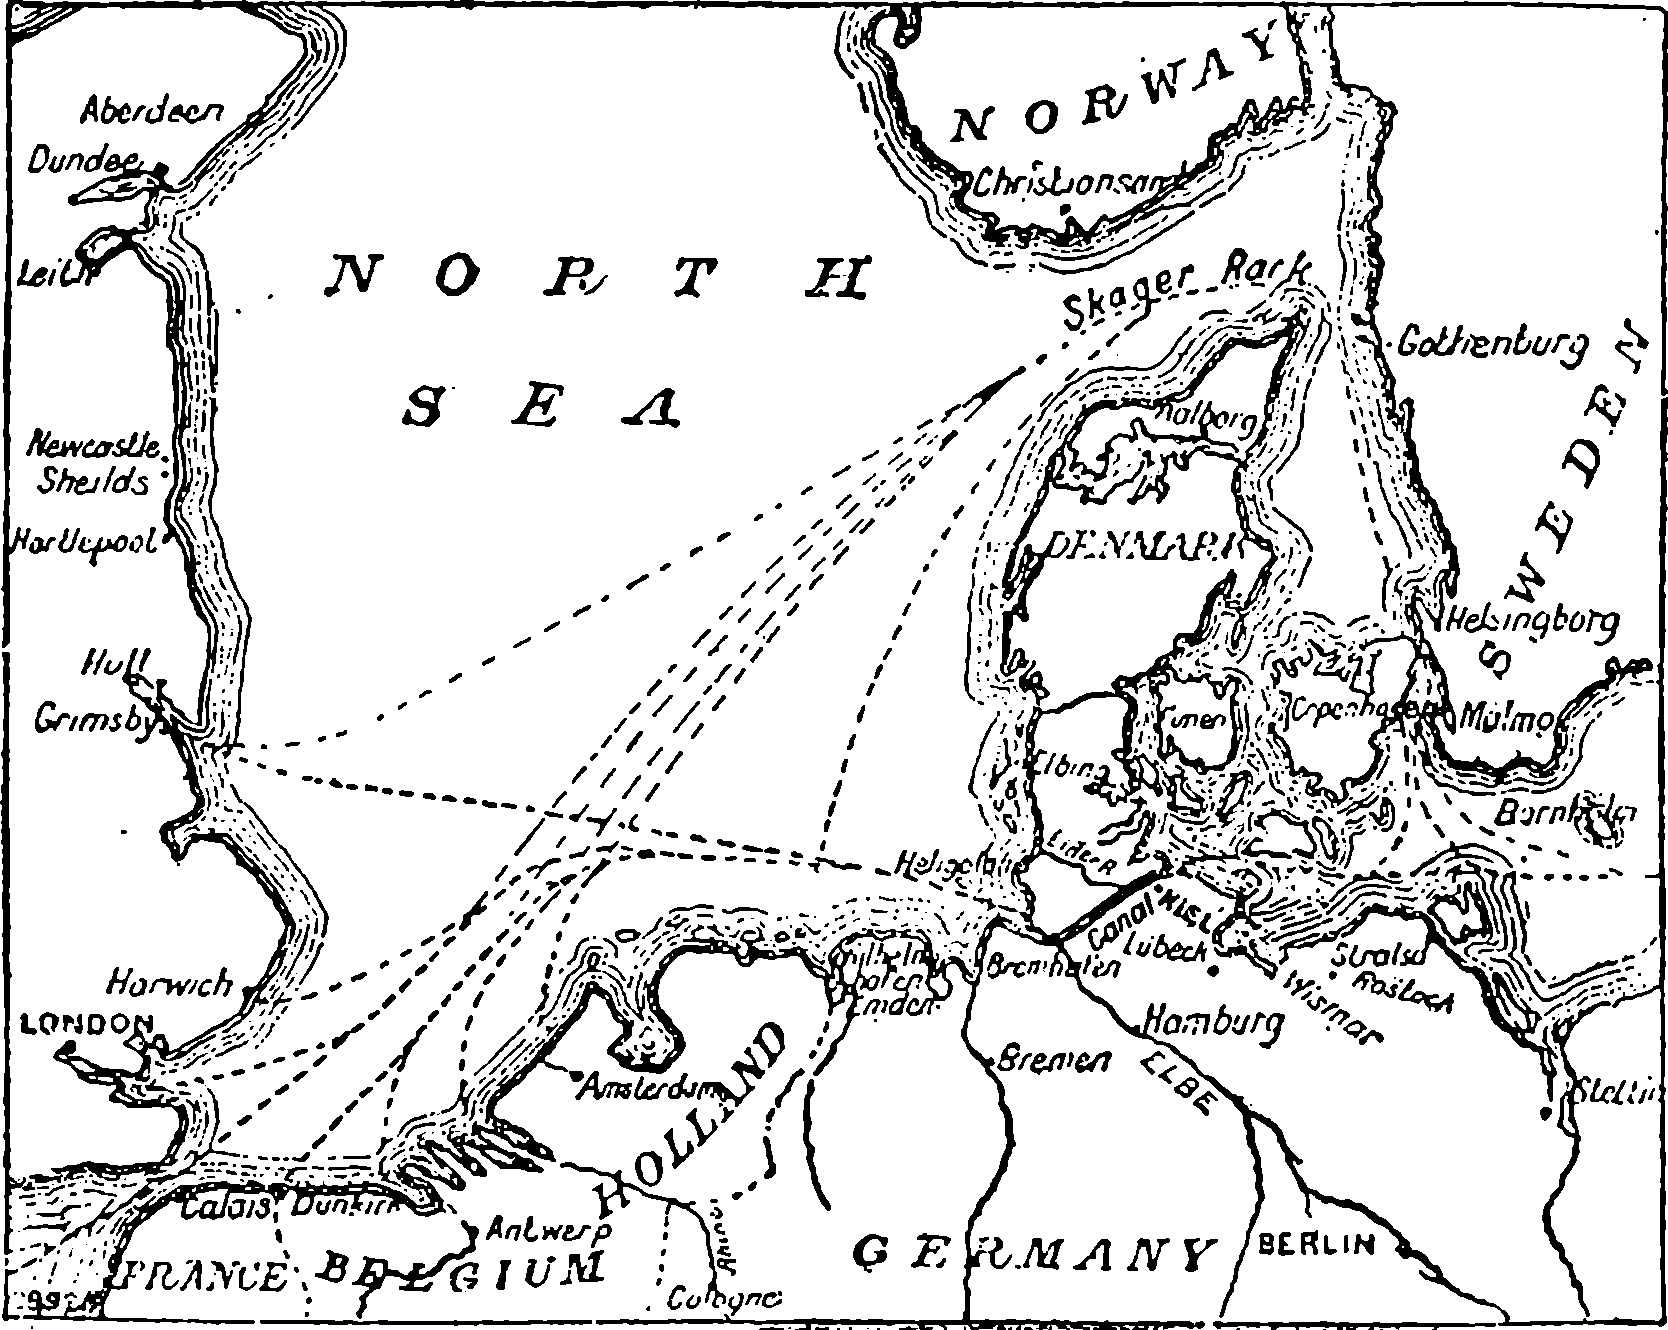
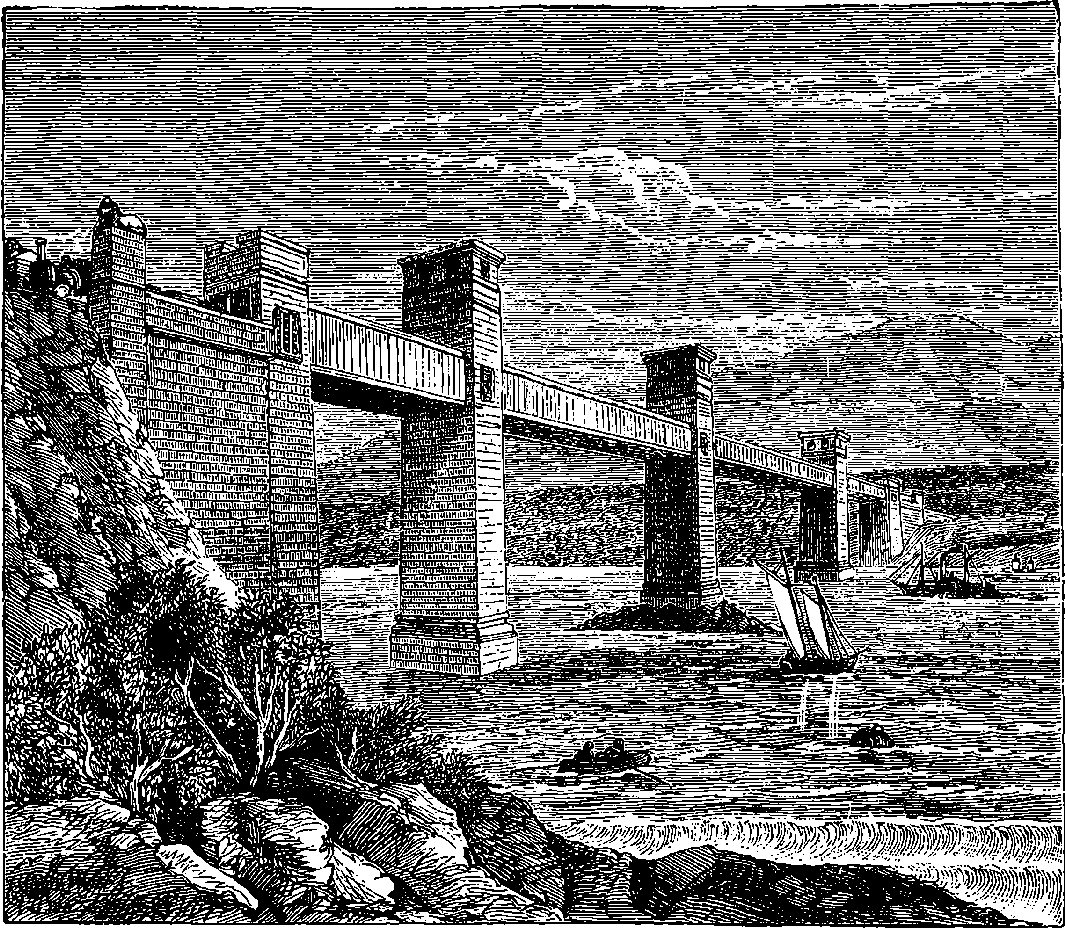
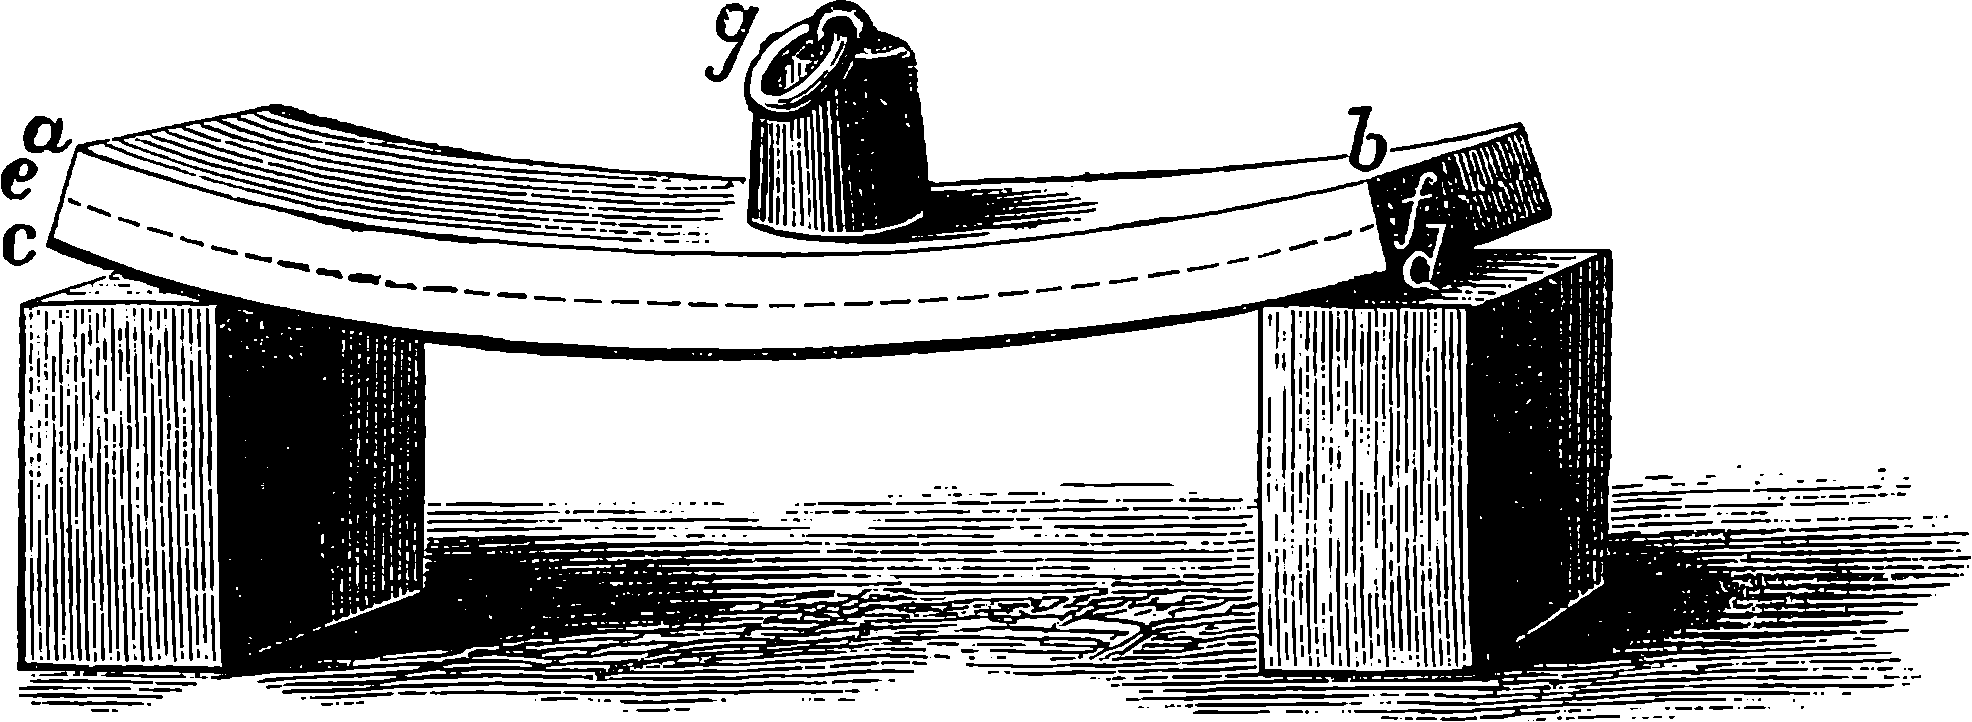
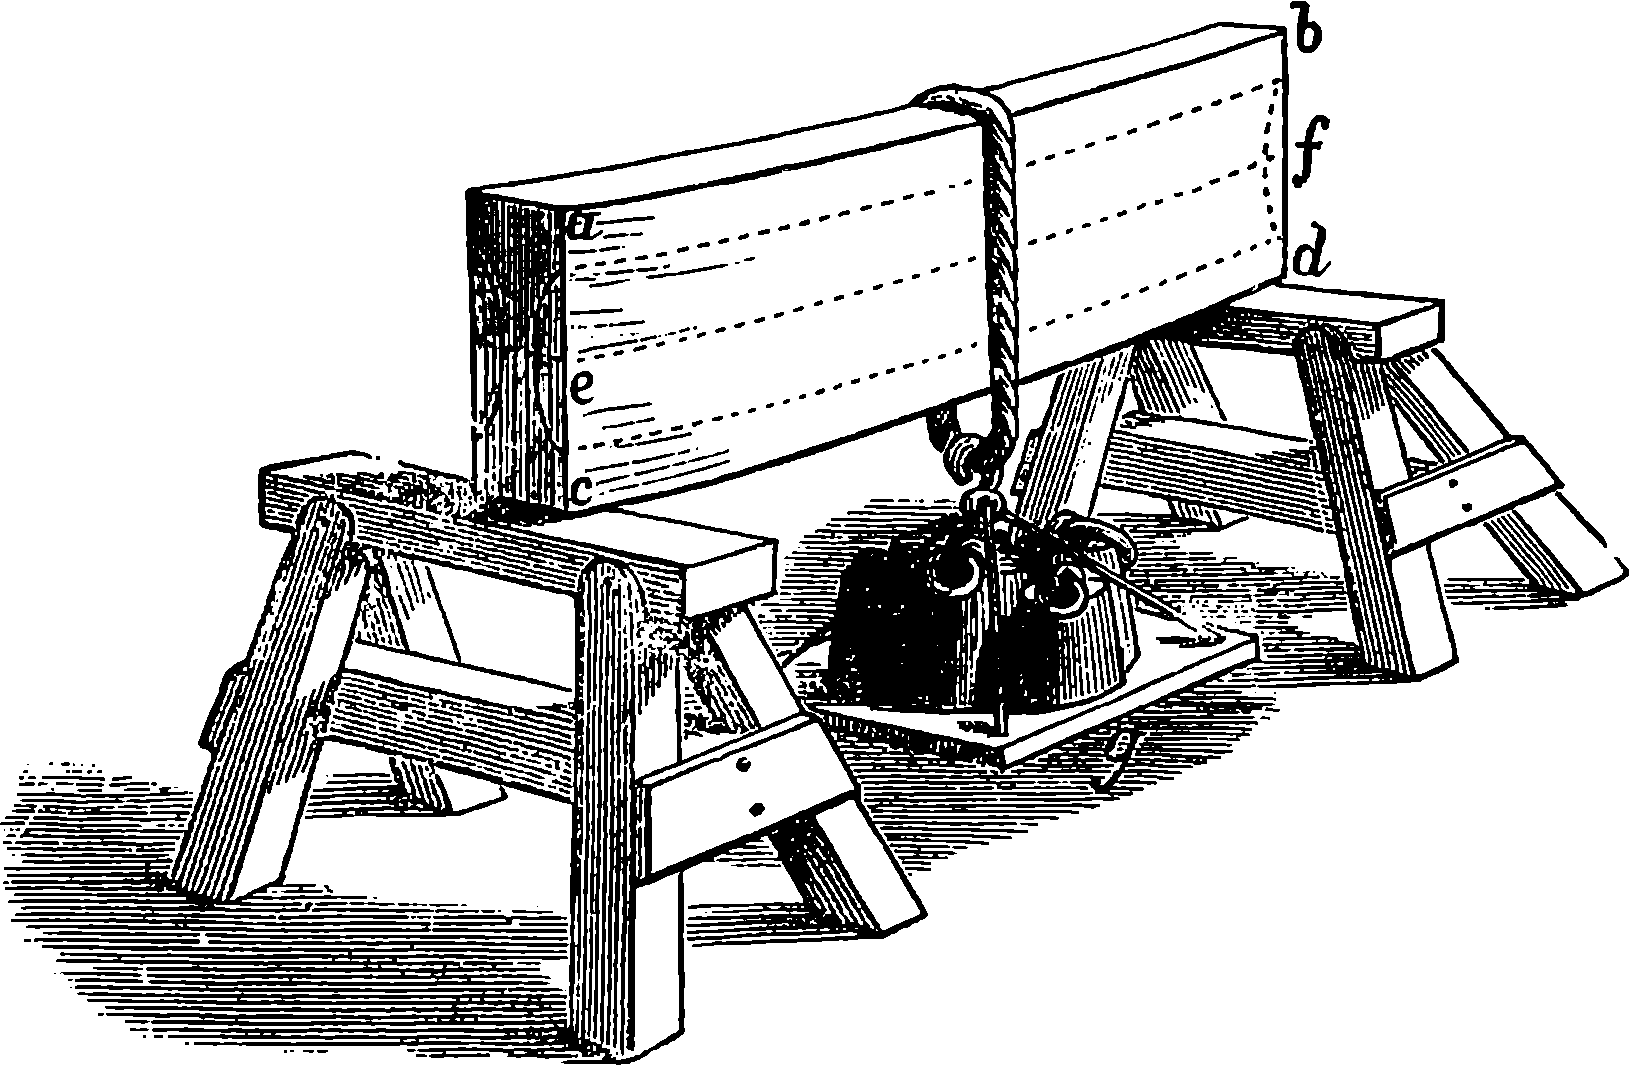
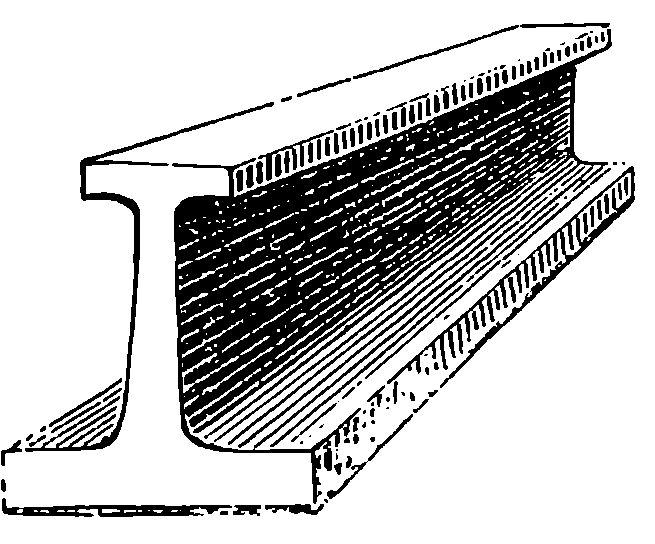
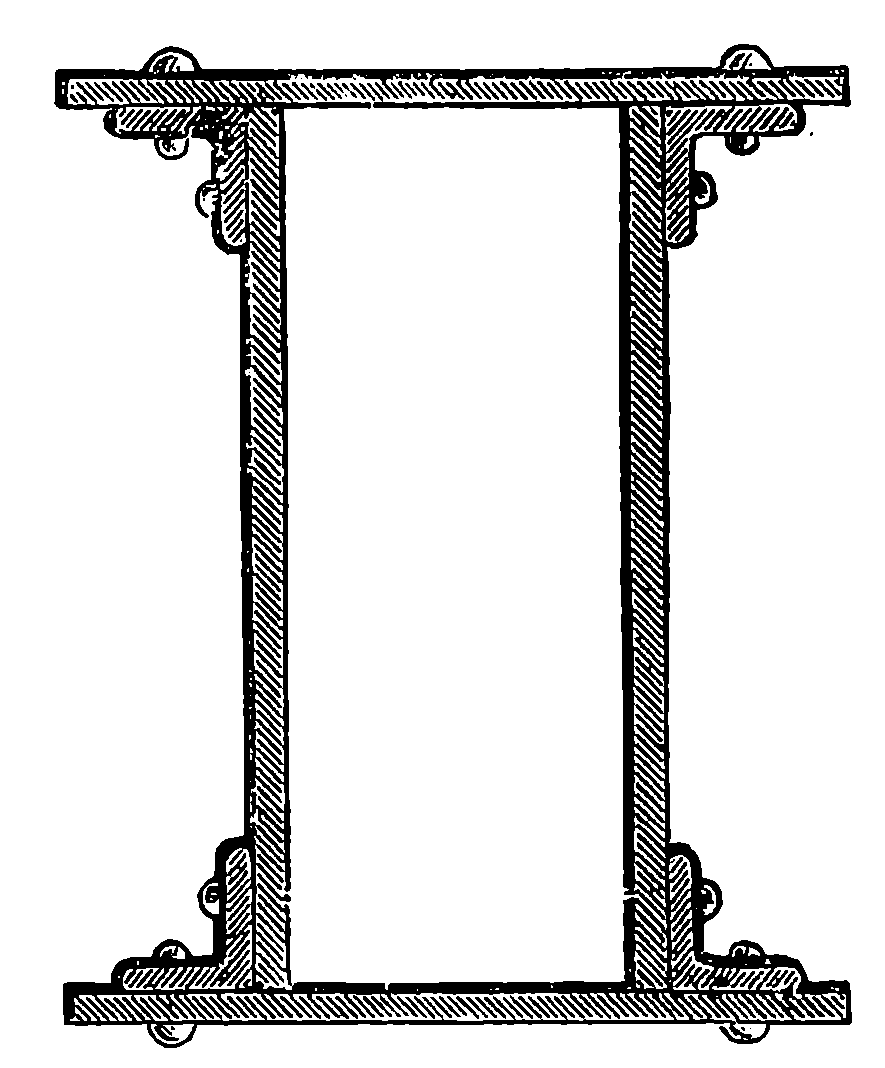
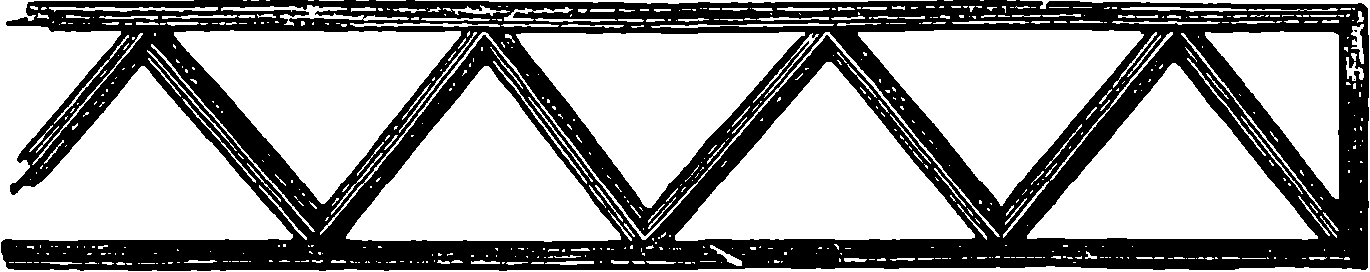
 . The cells are also formed
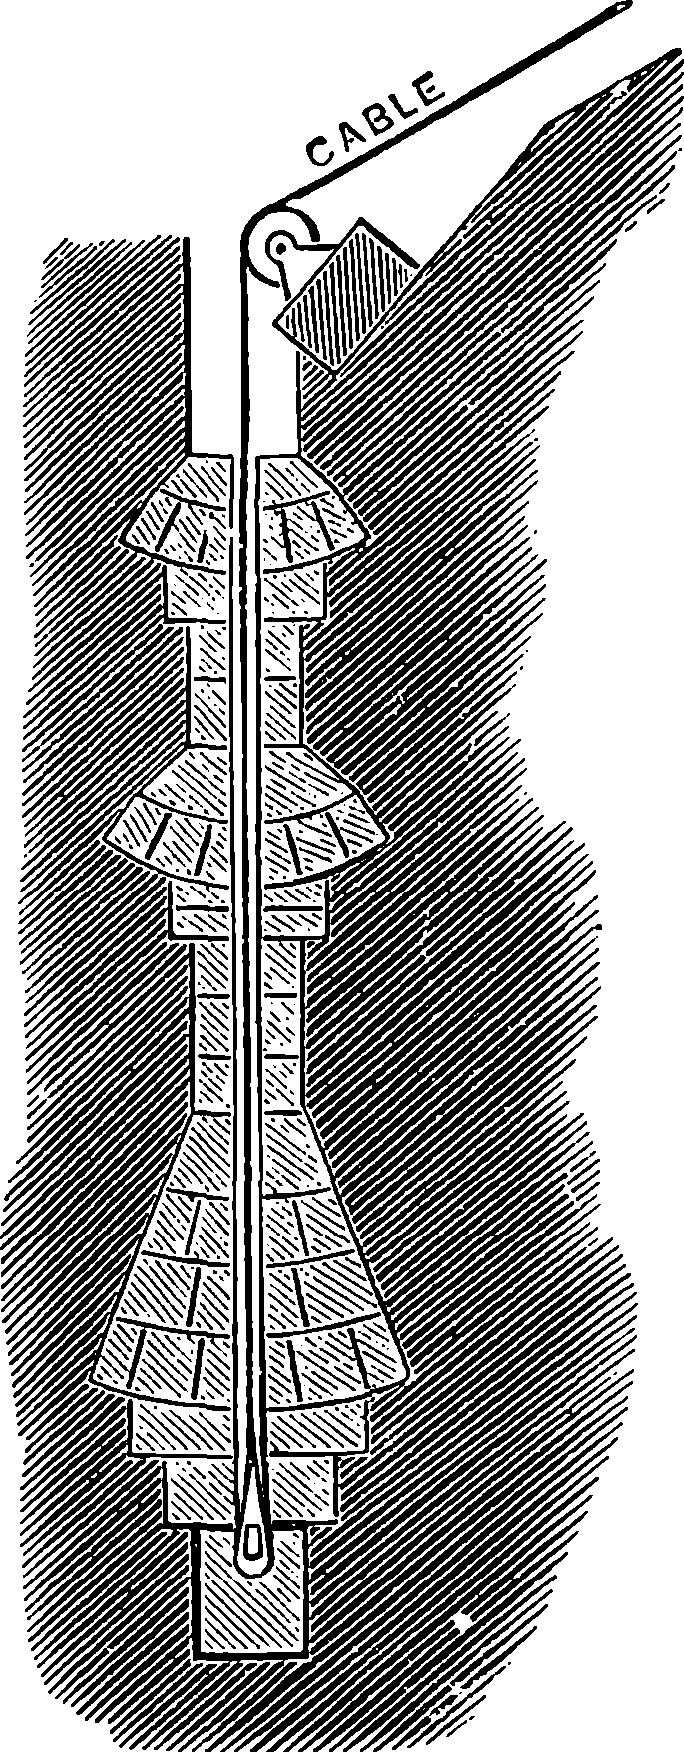
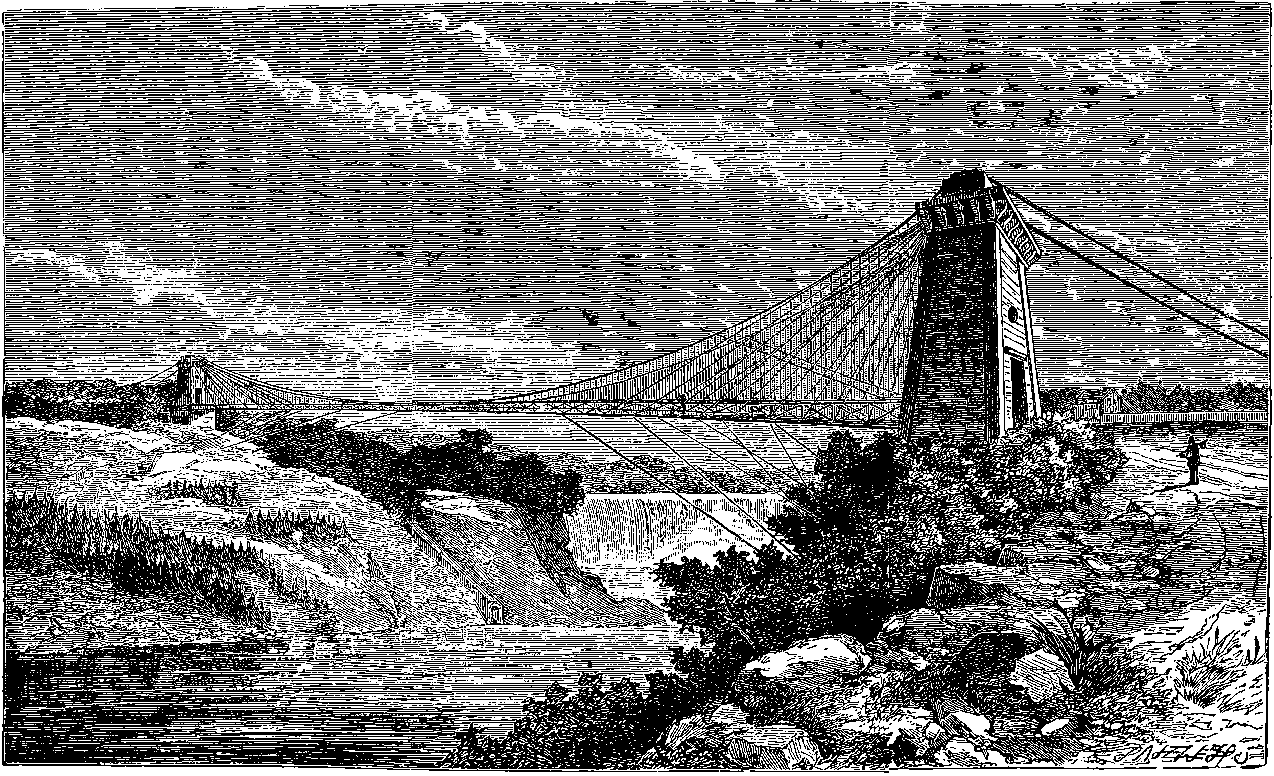
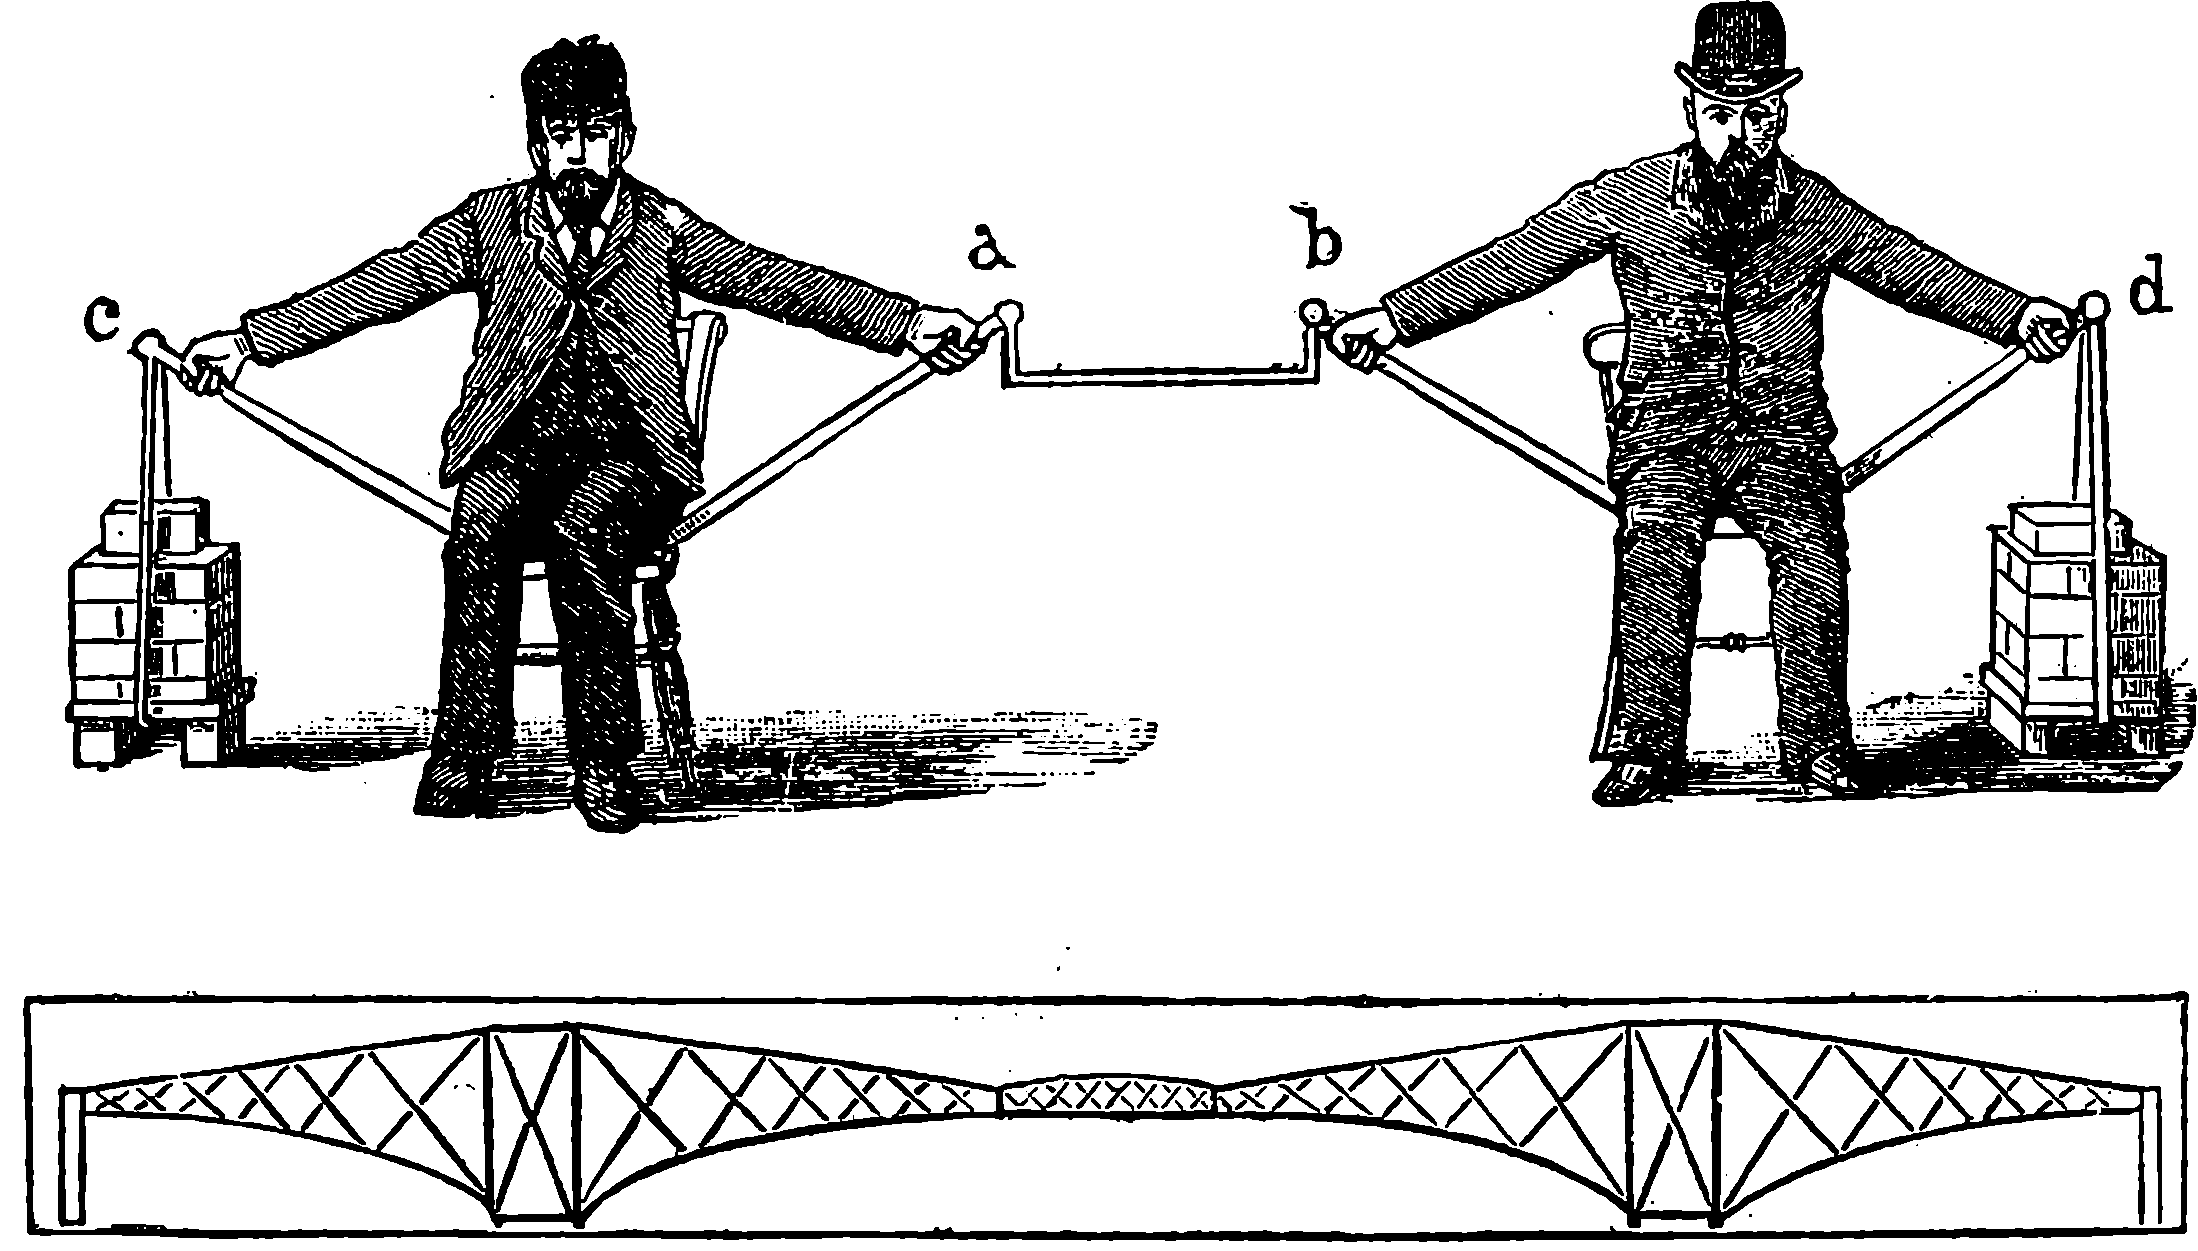
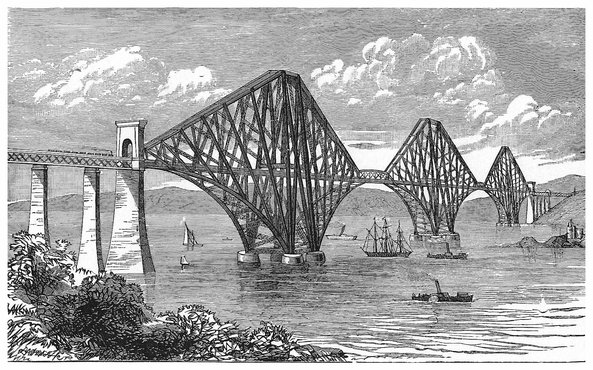
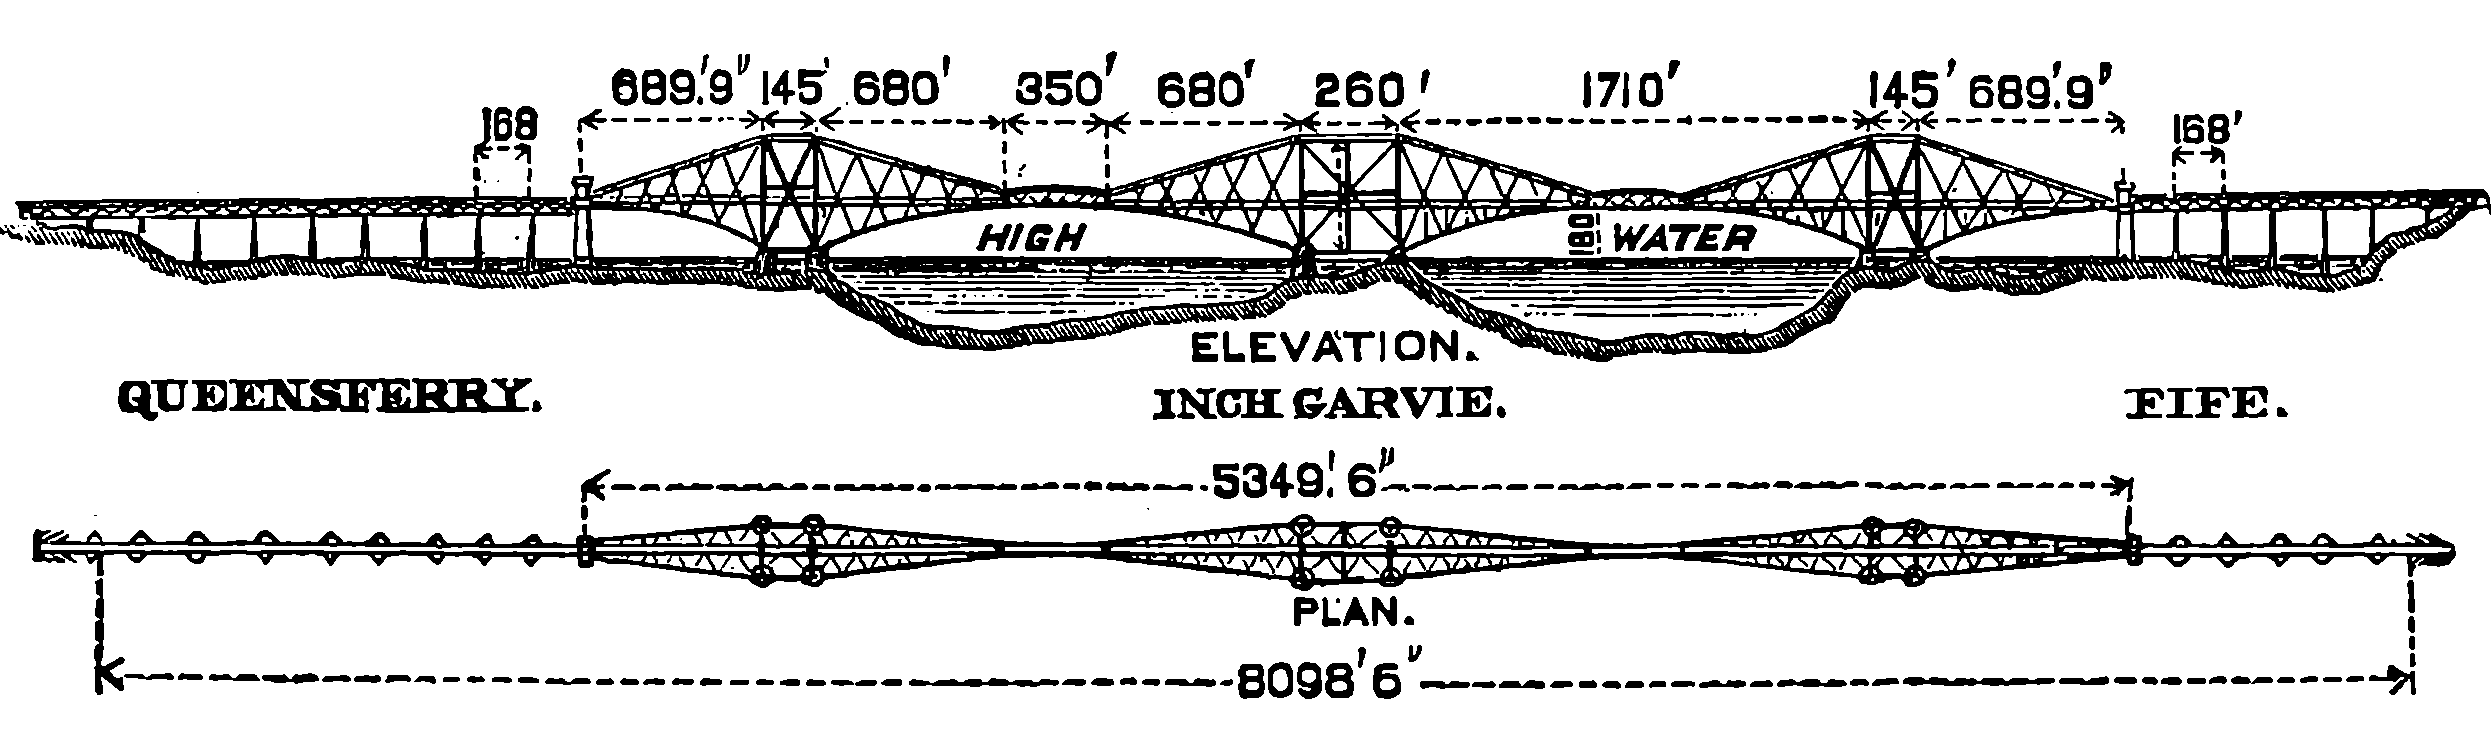
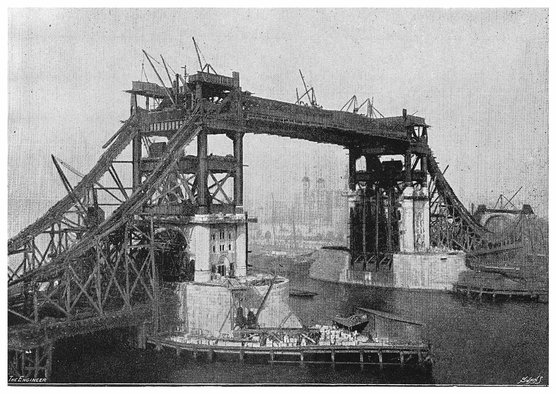
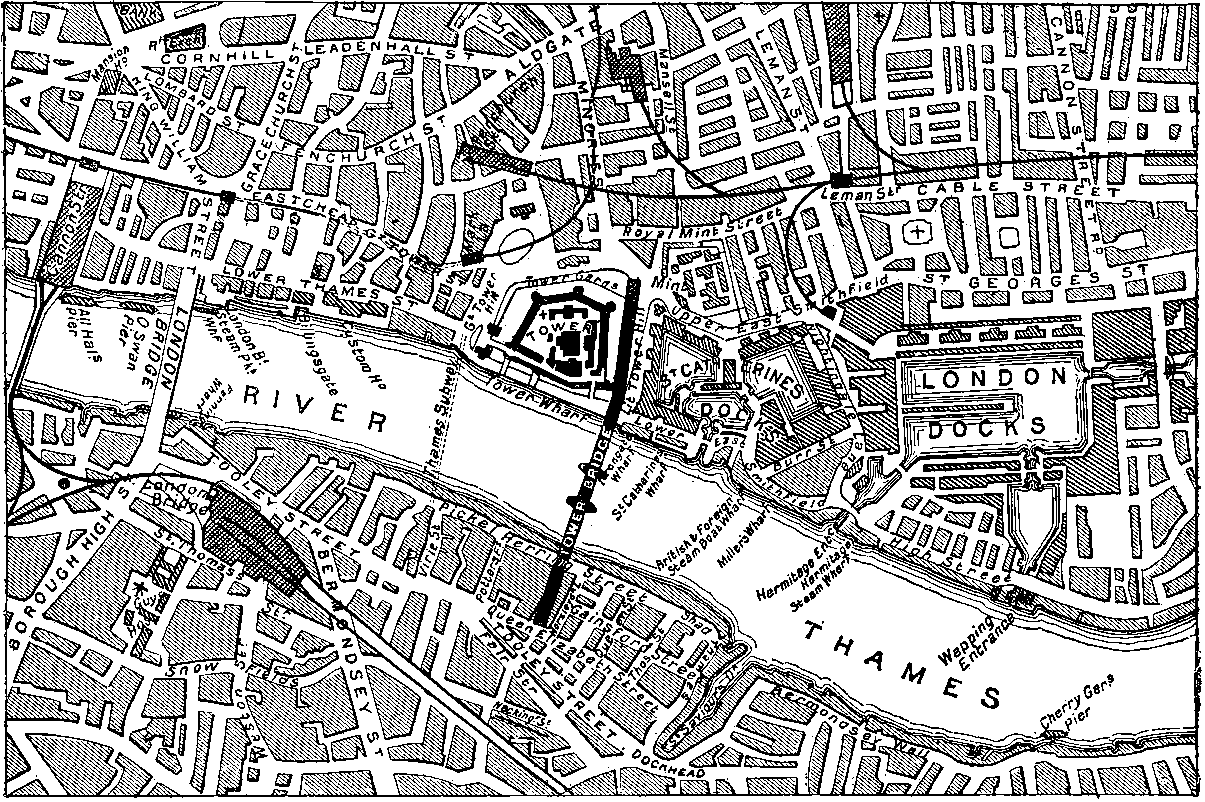
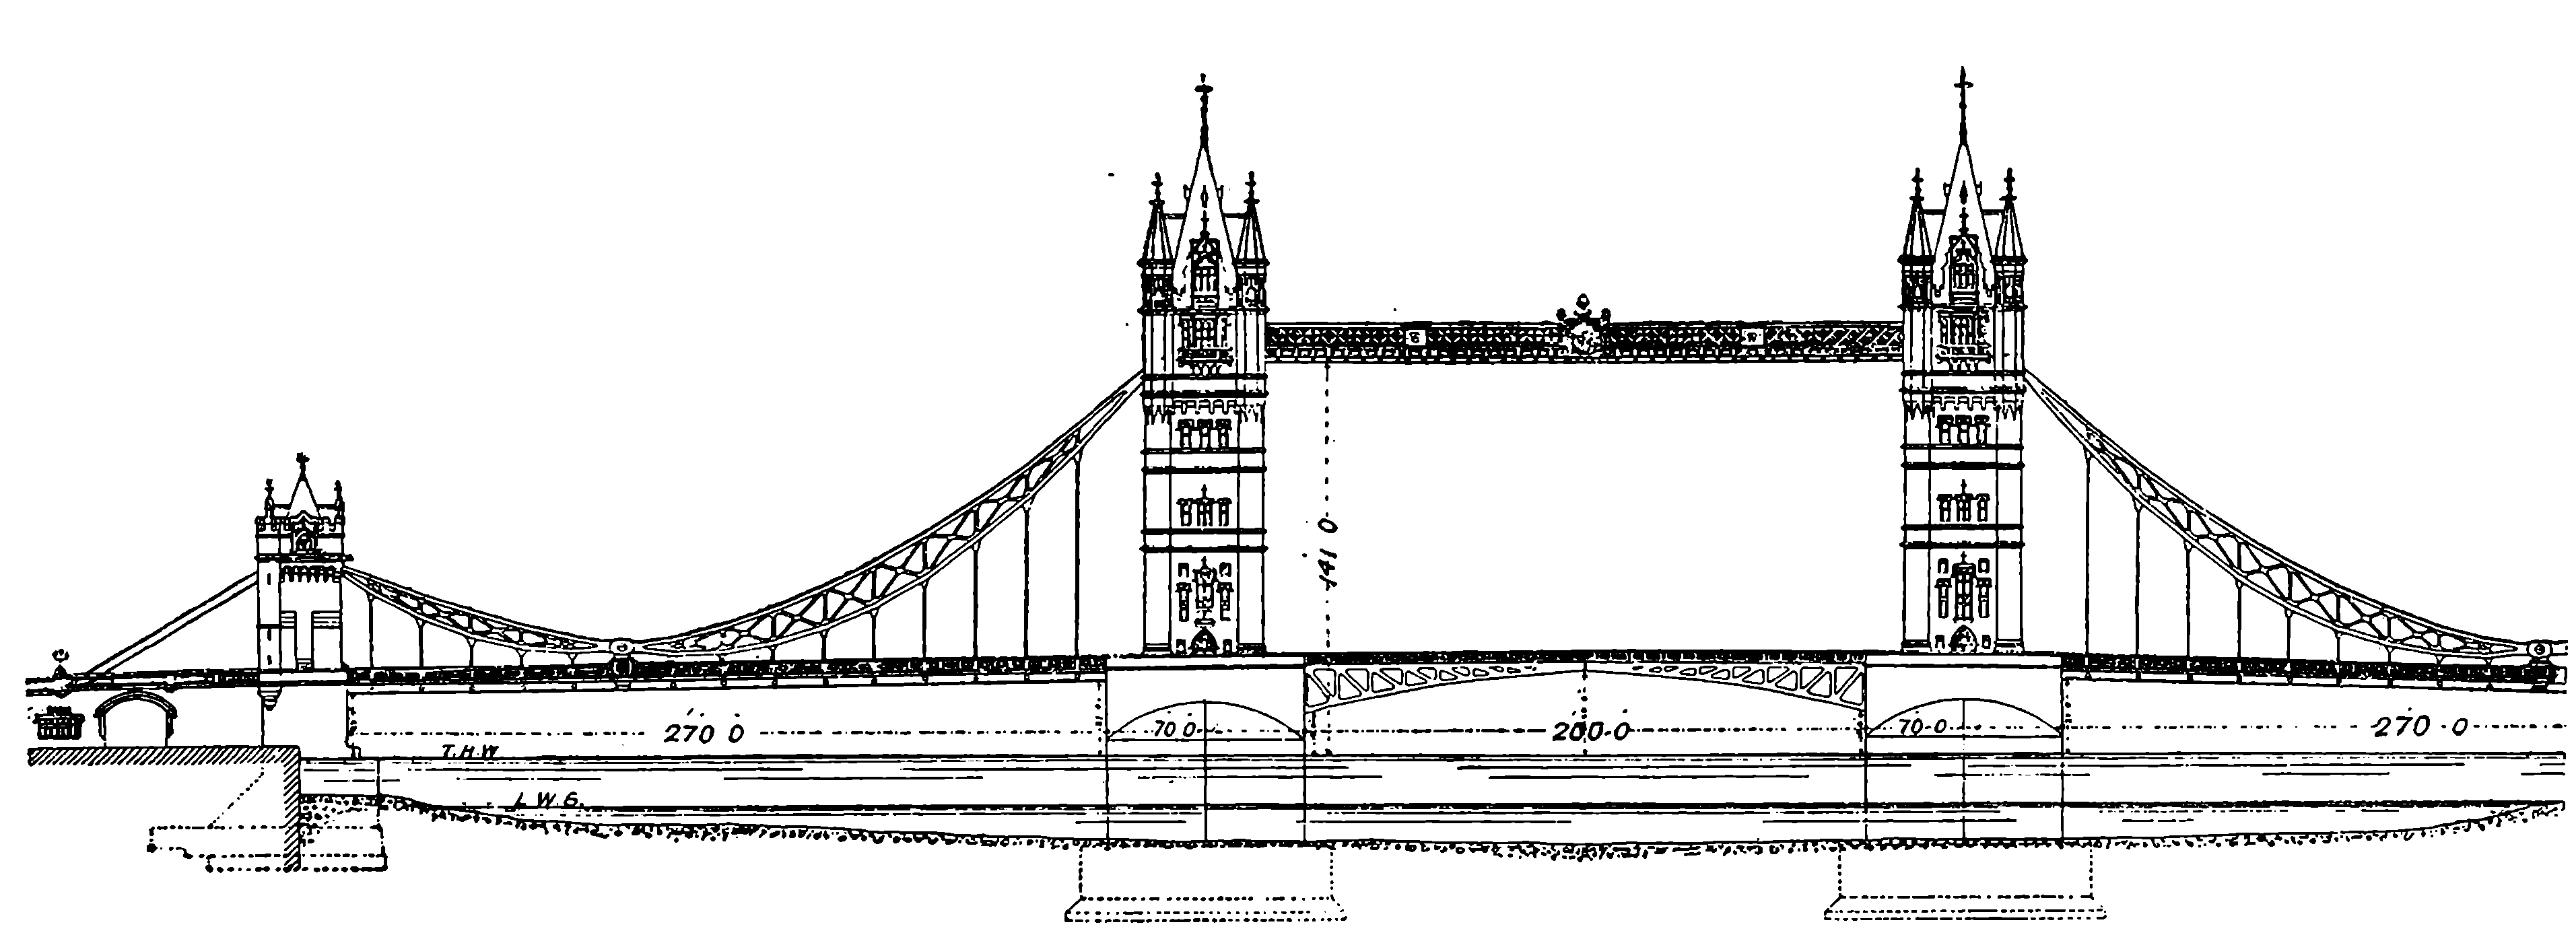
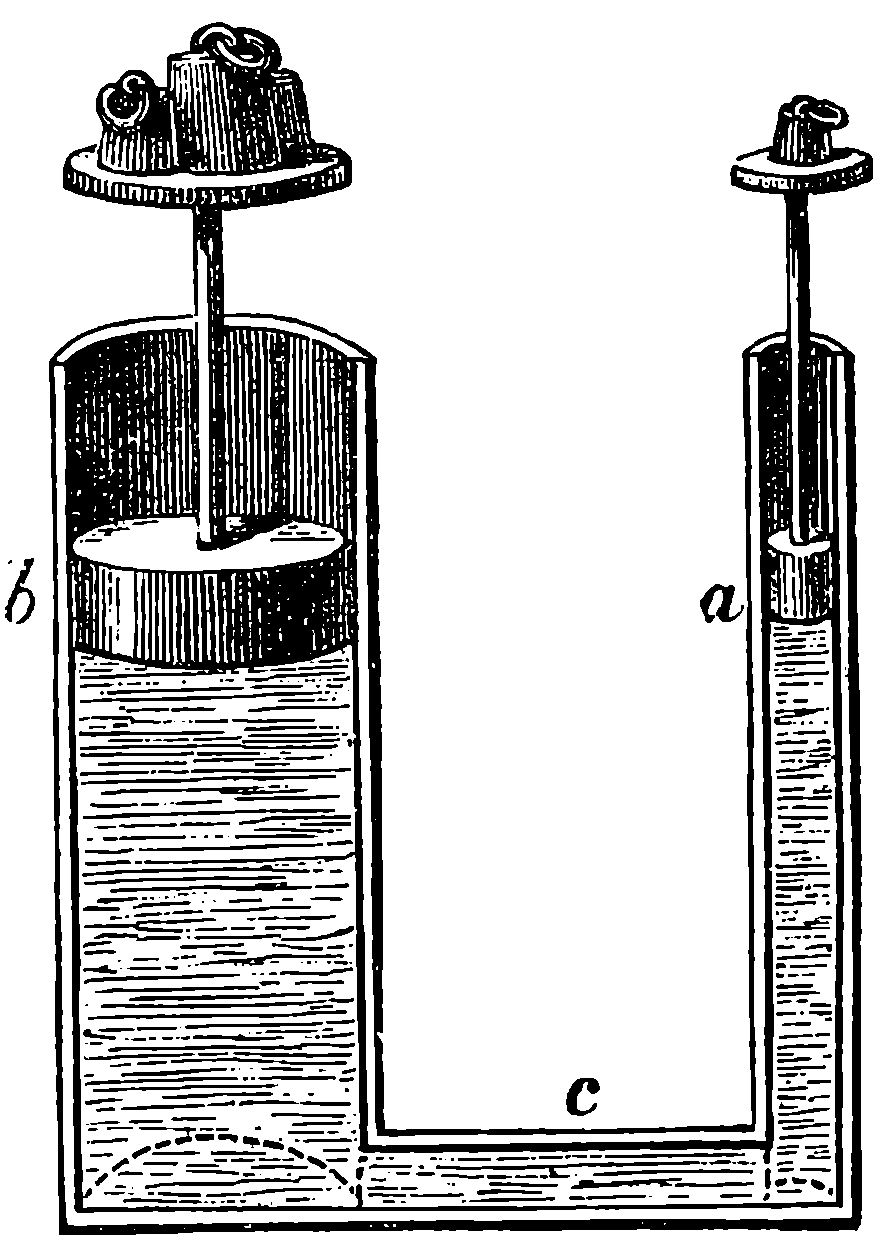
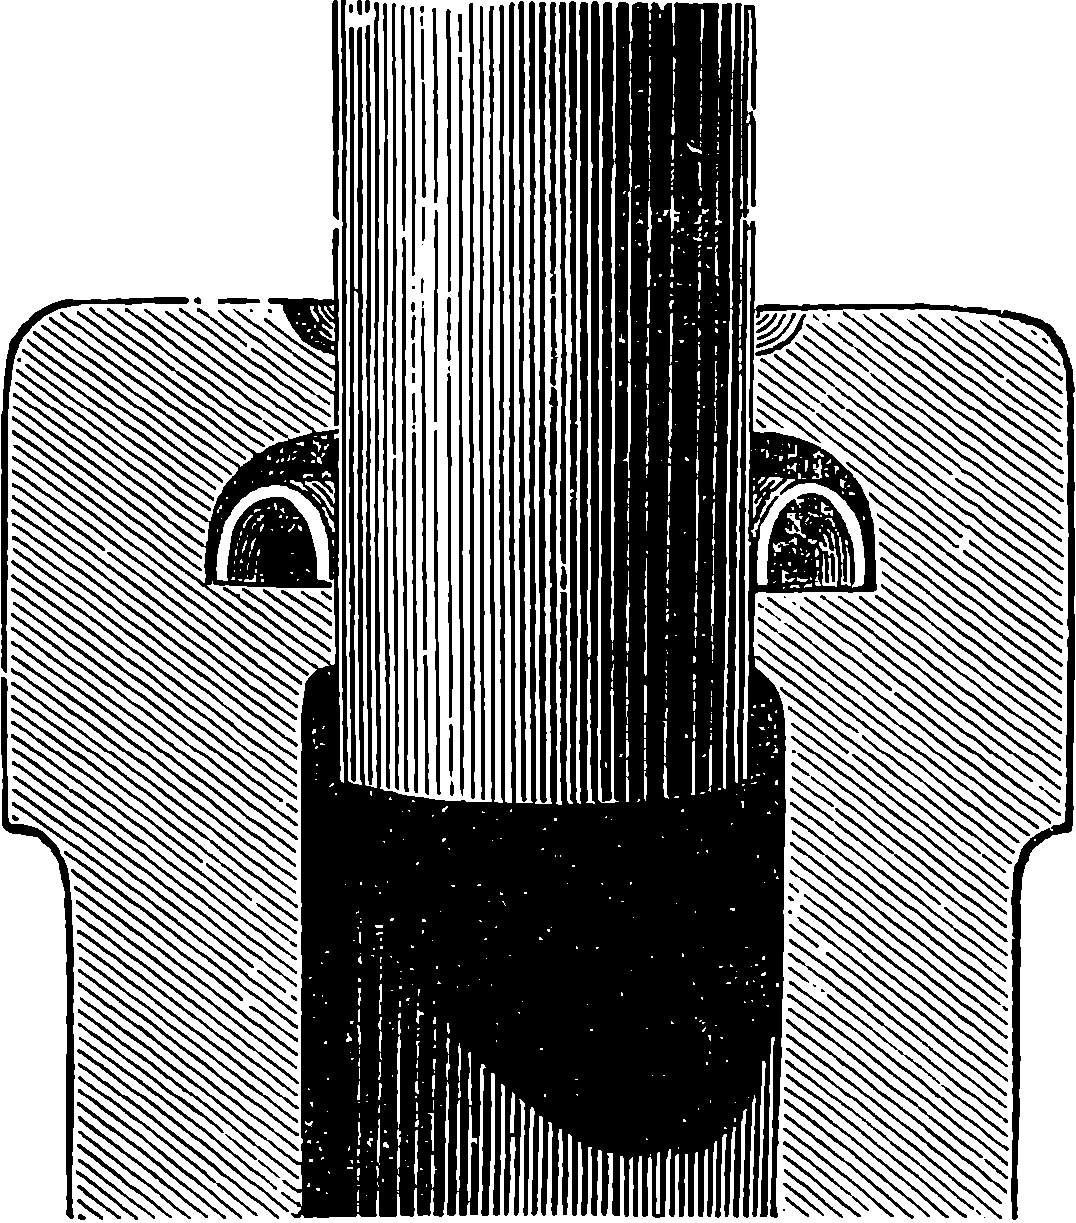
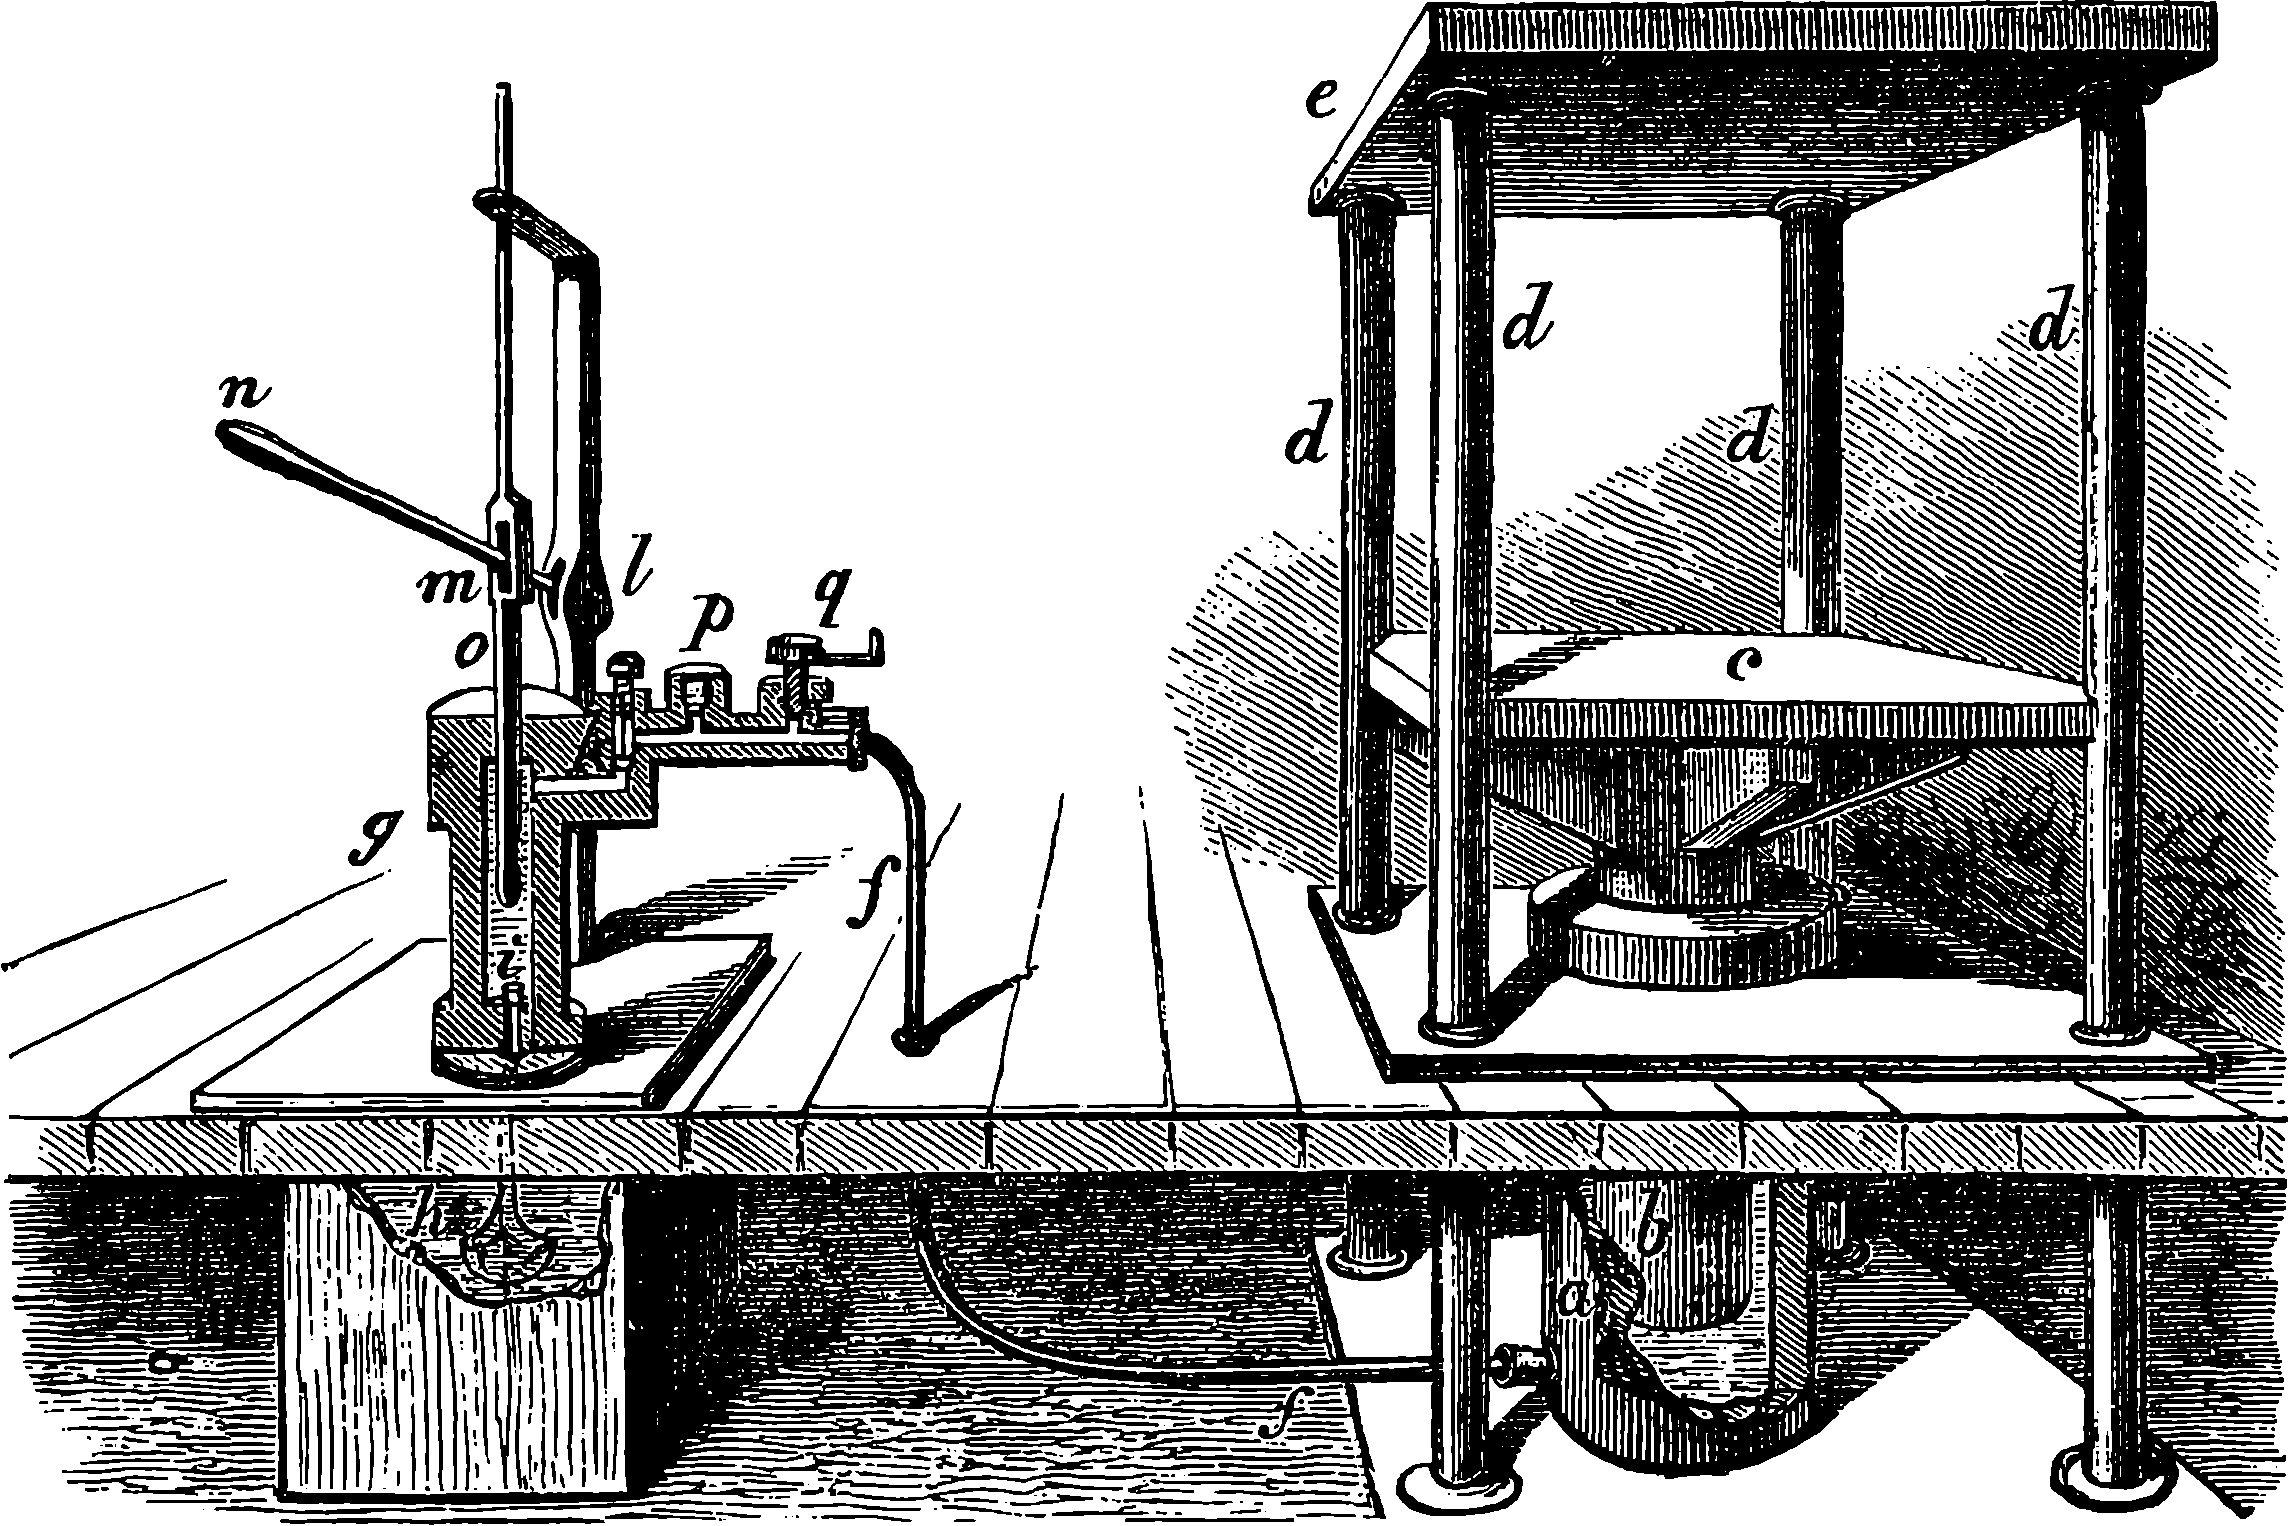
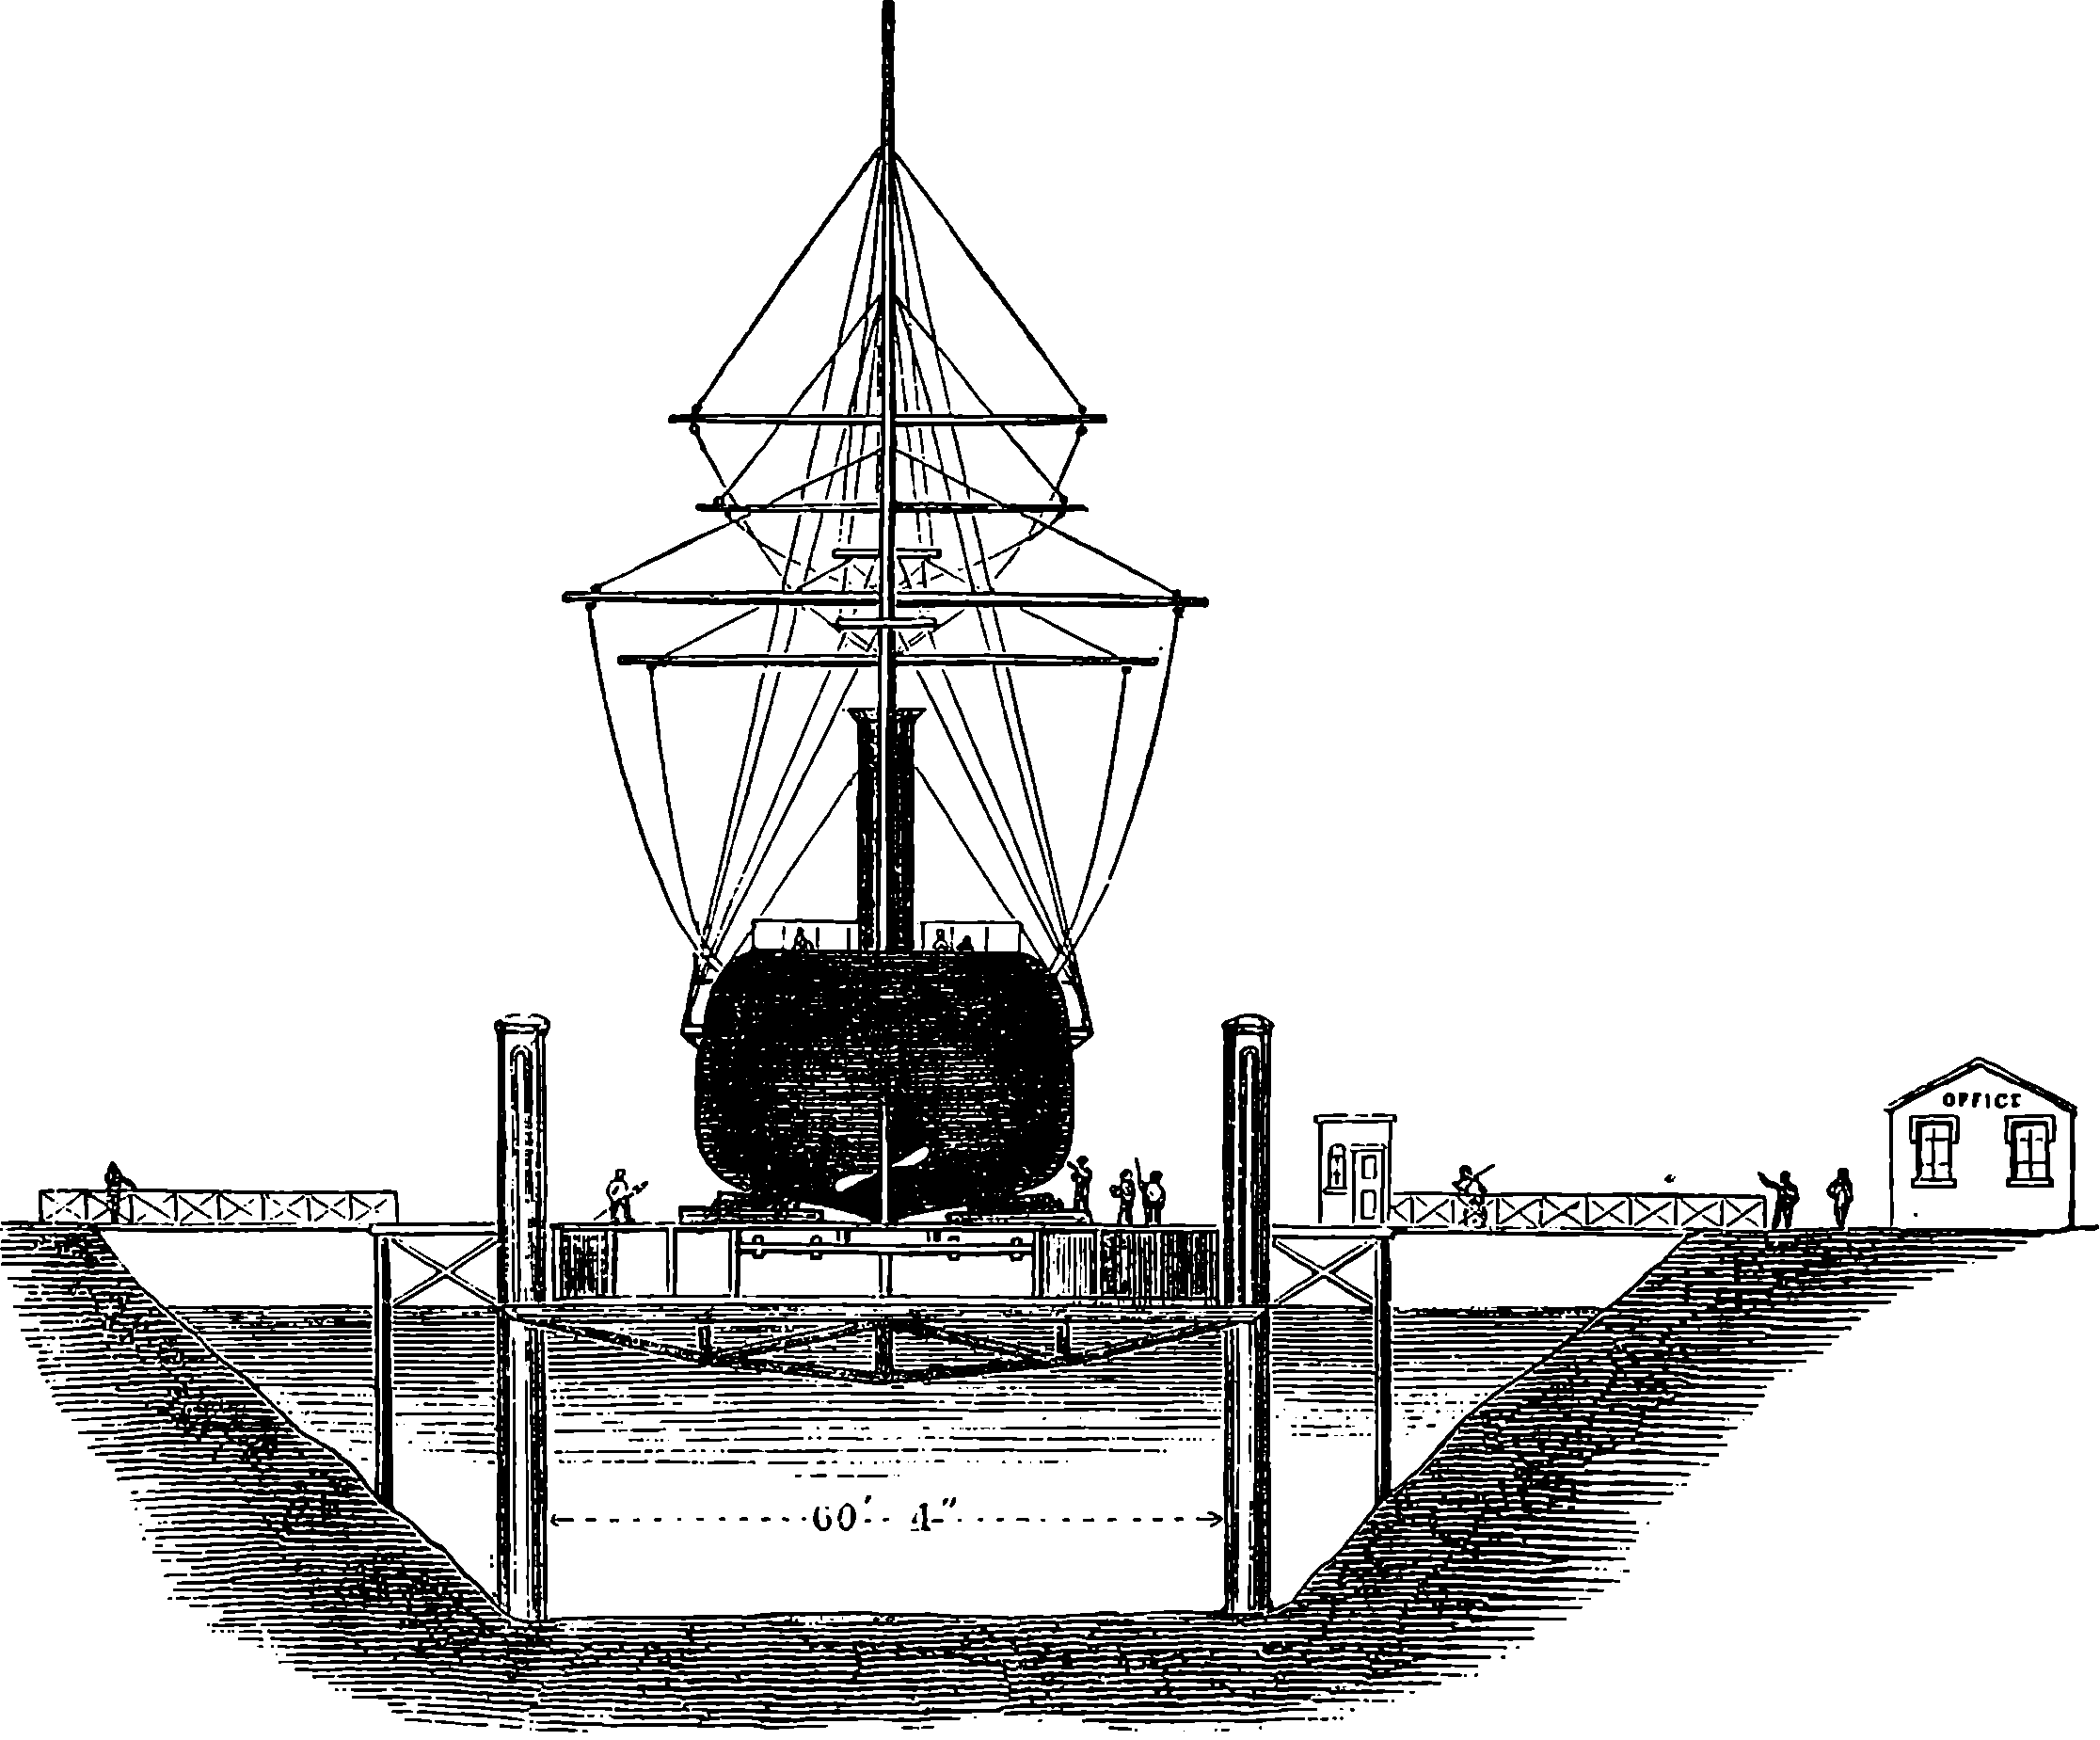
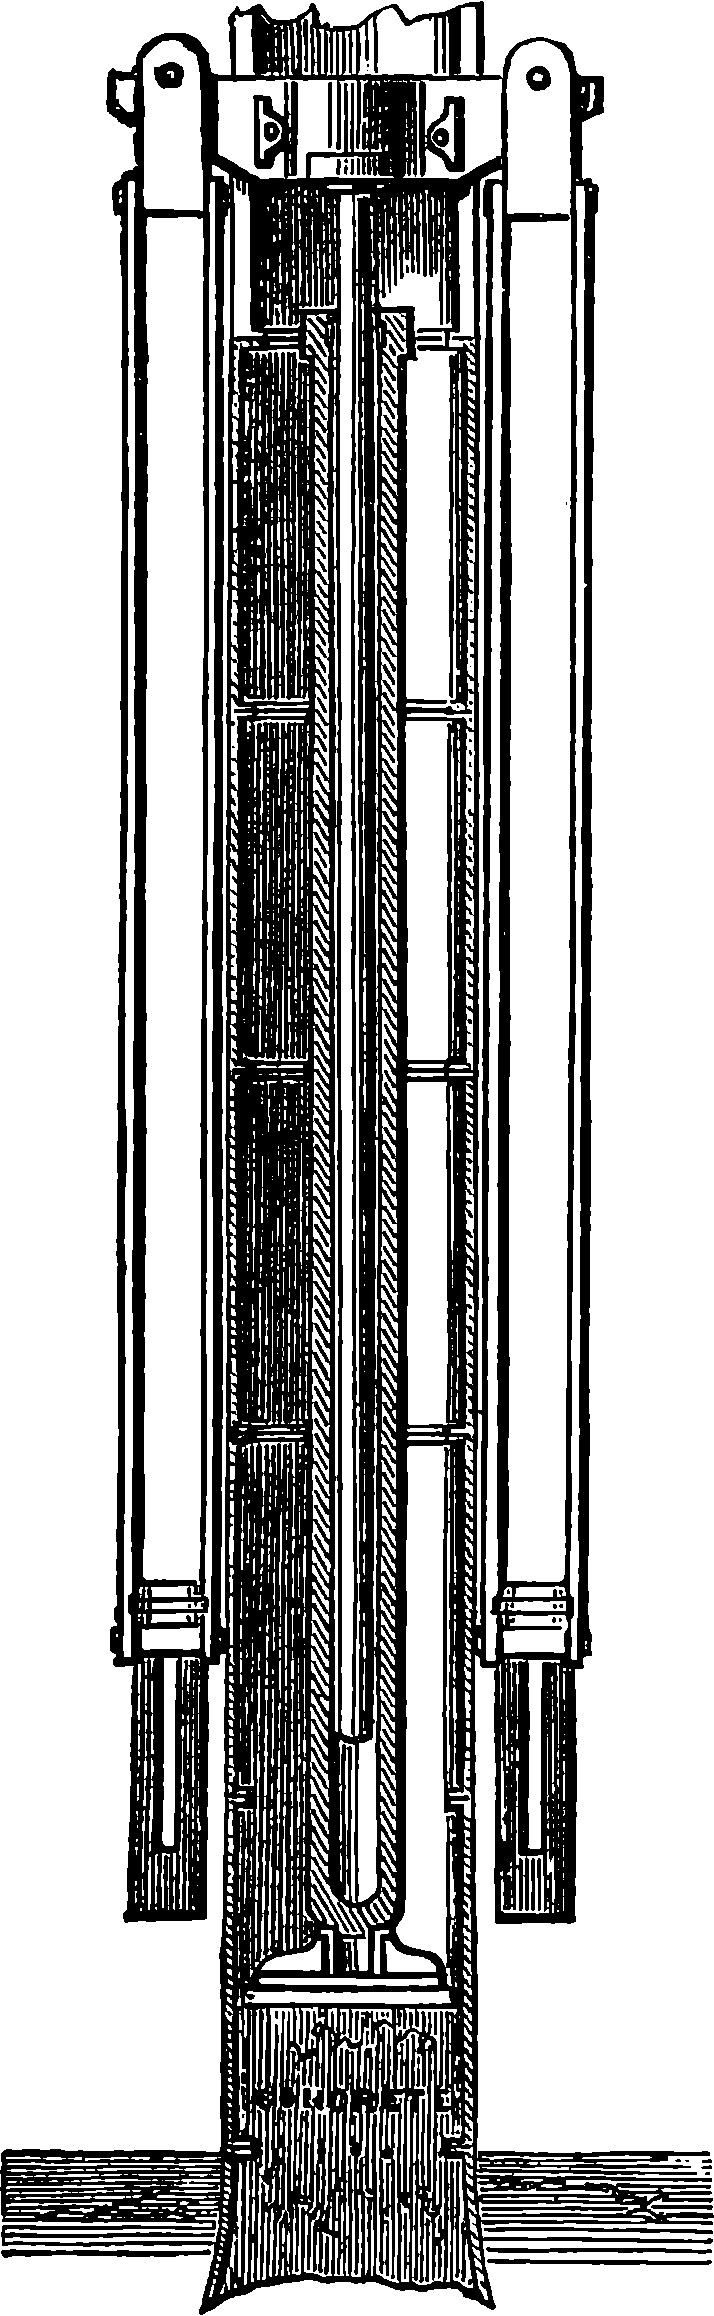
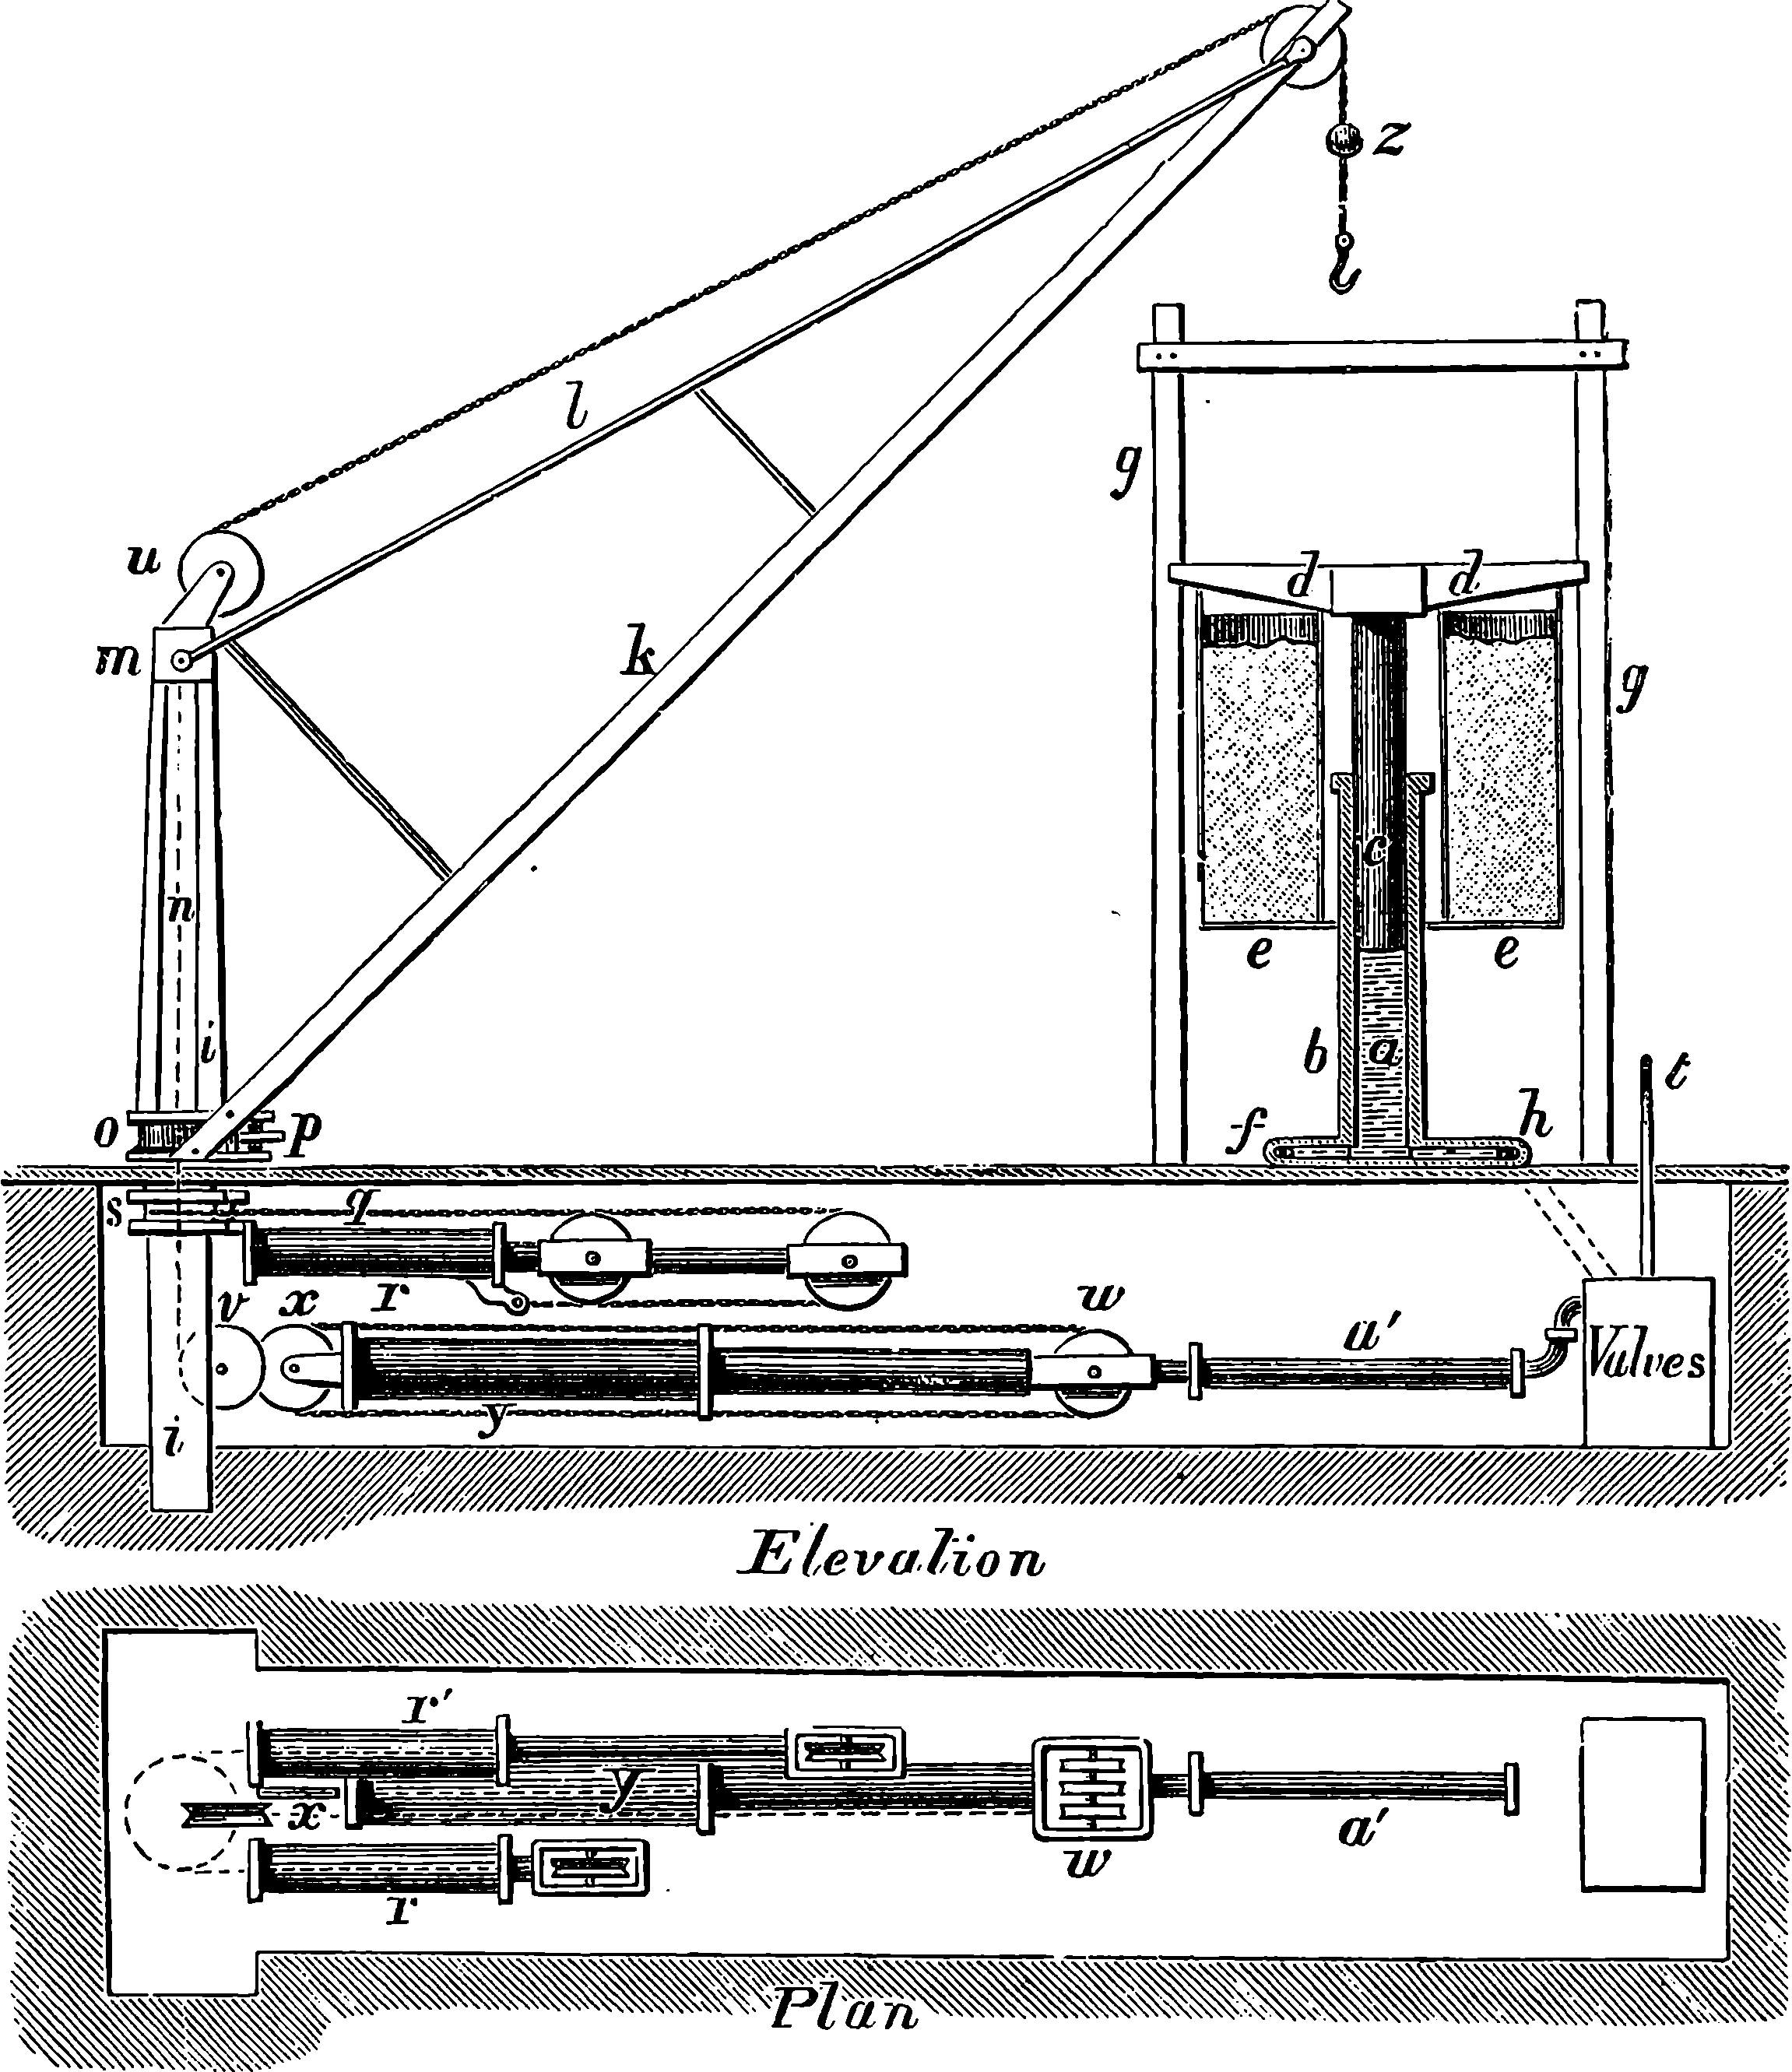
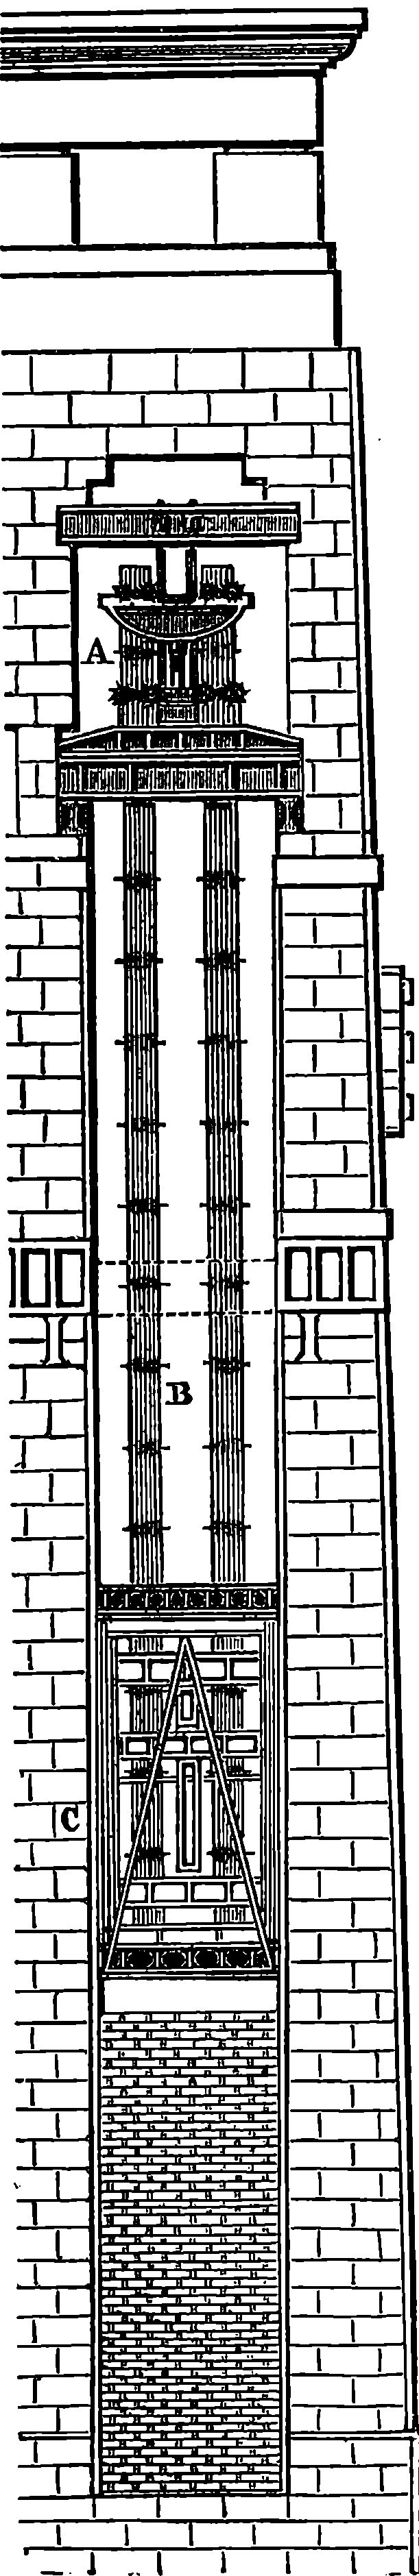
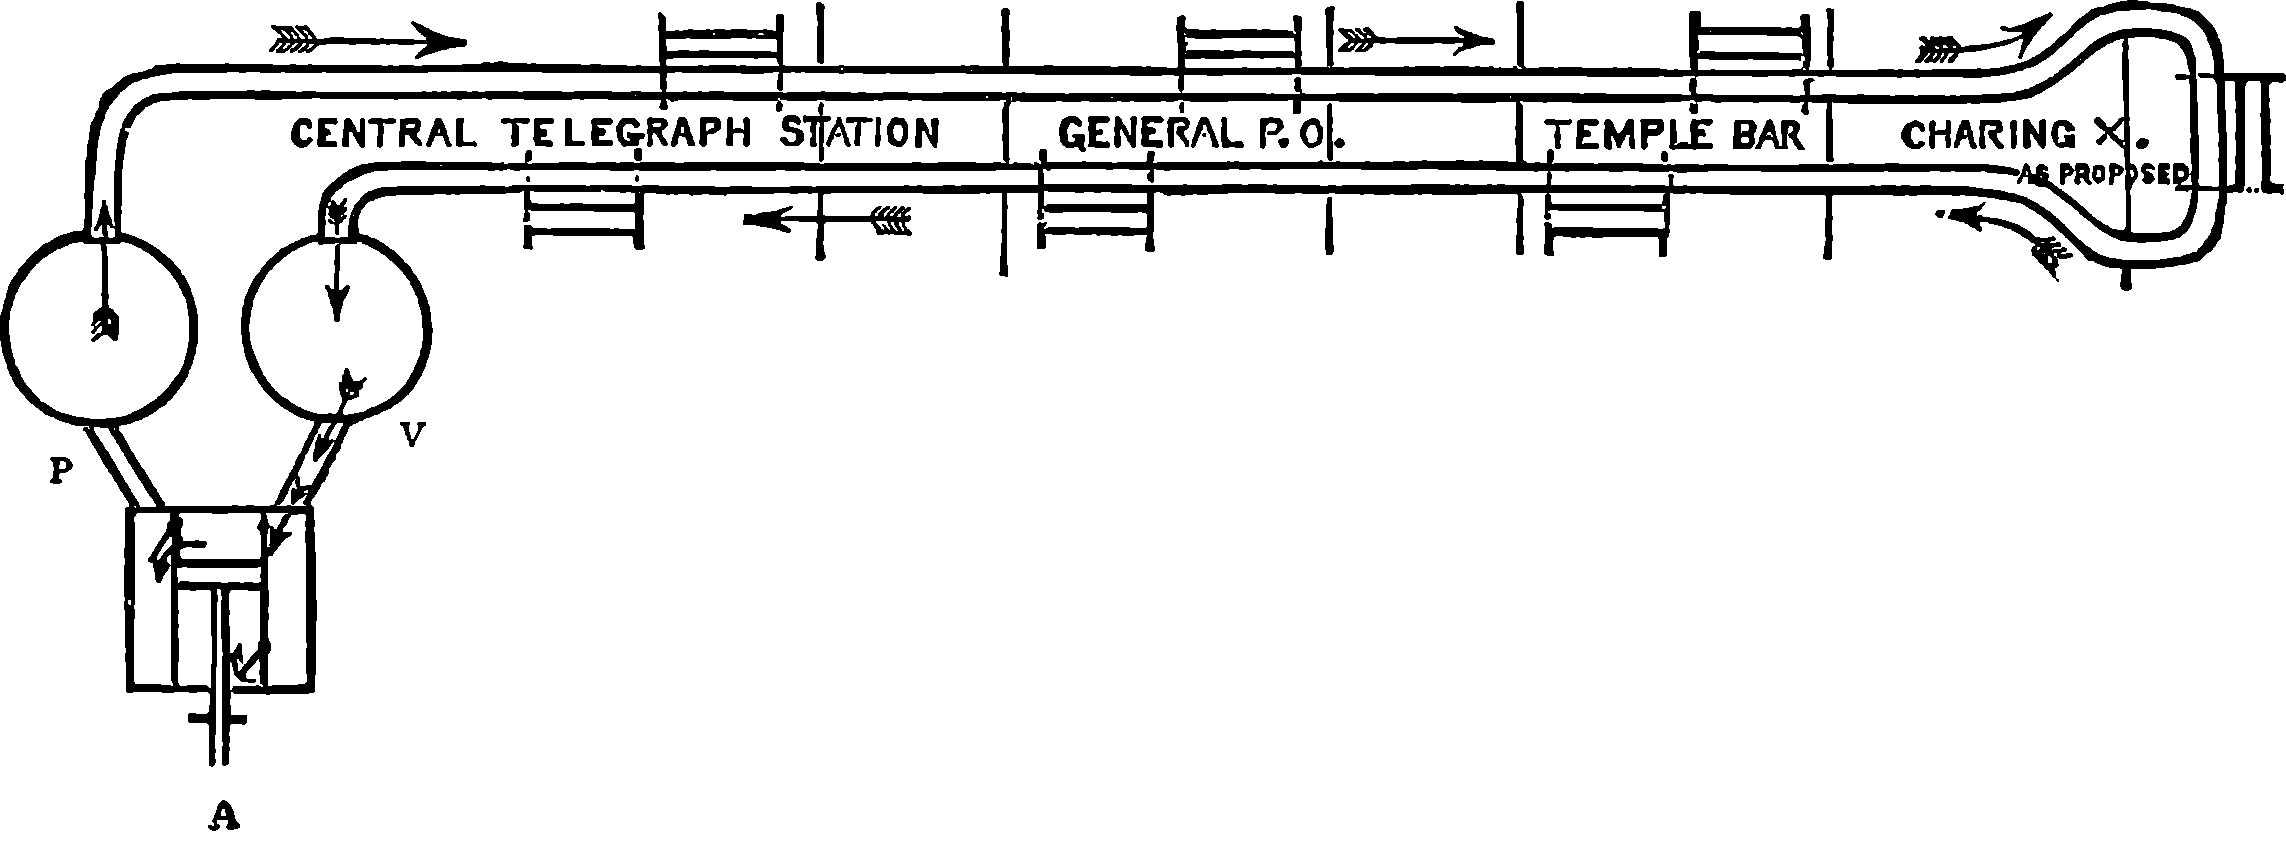
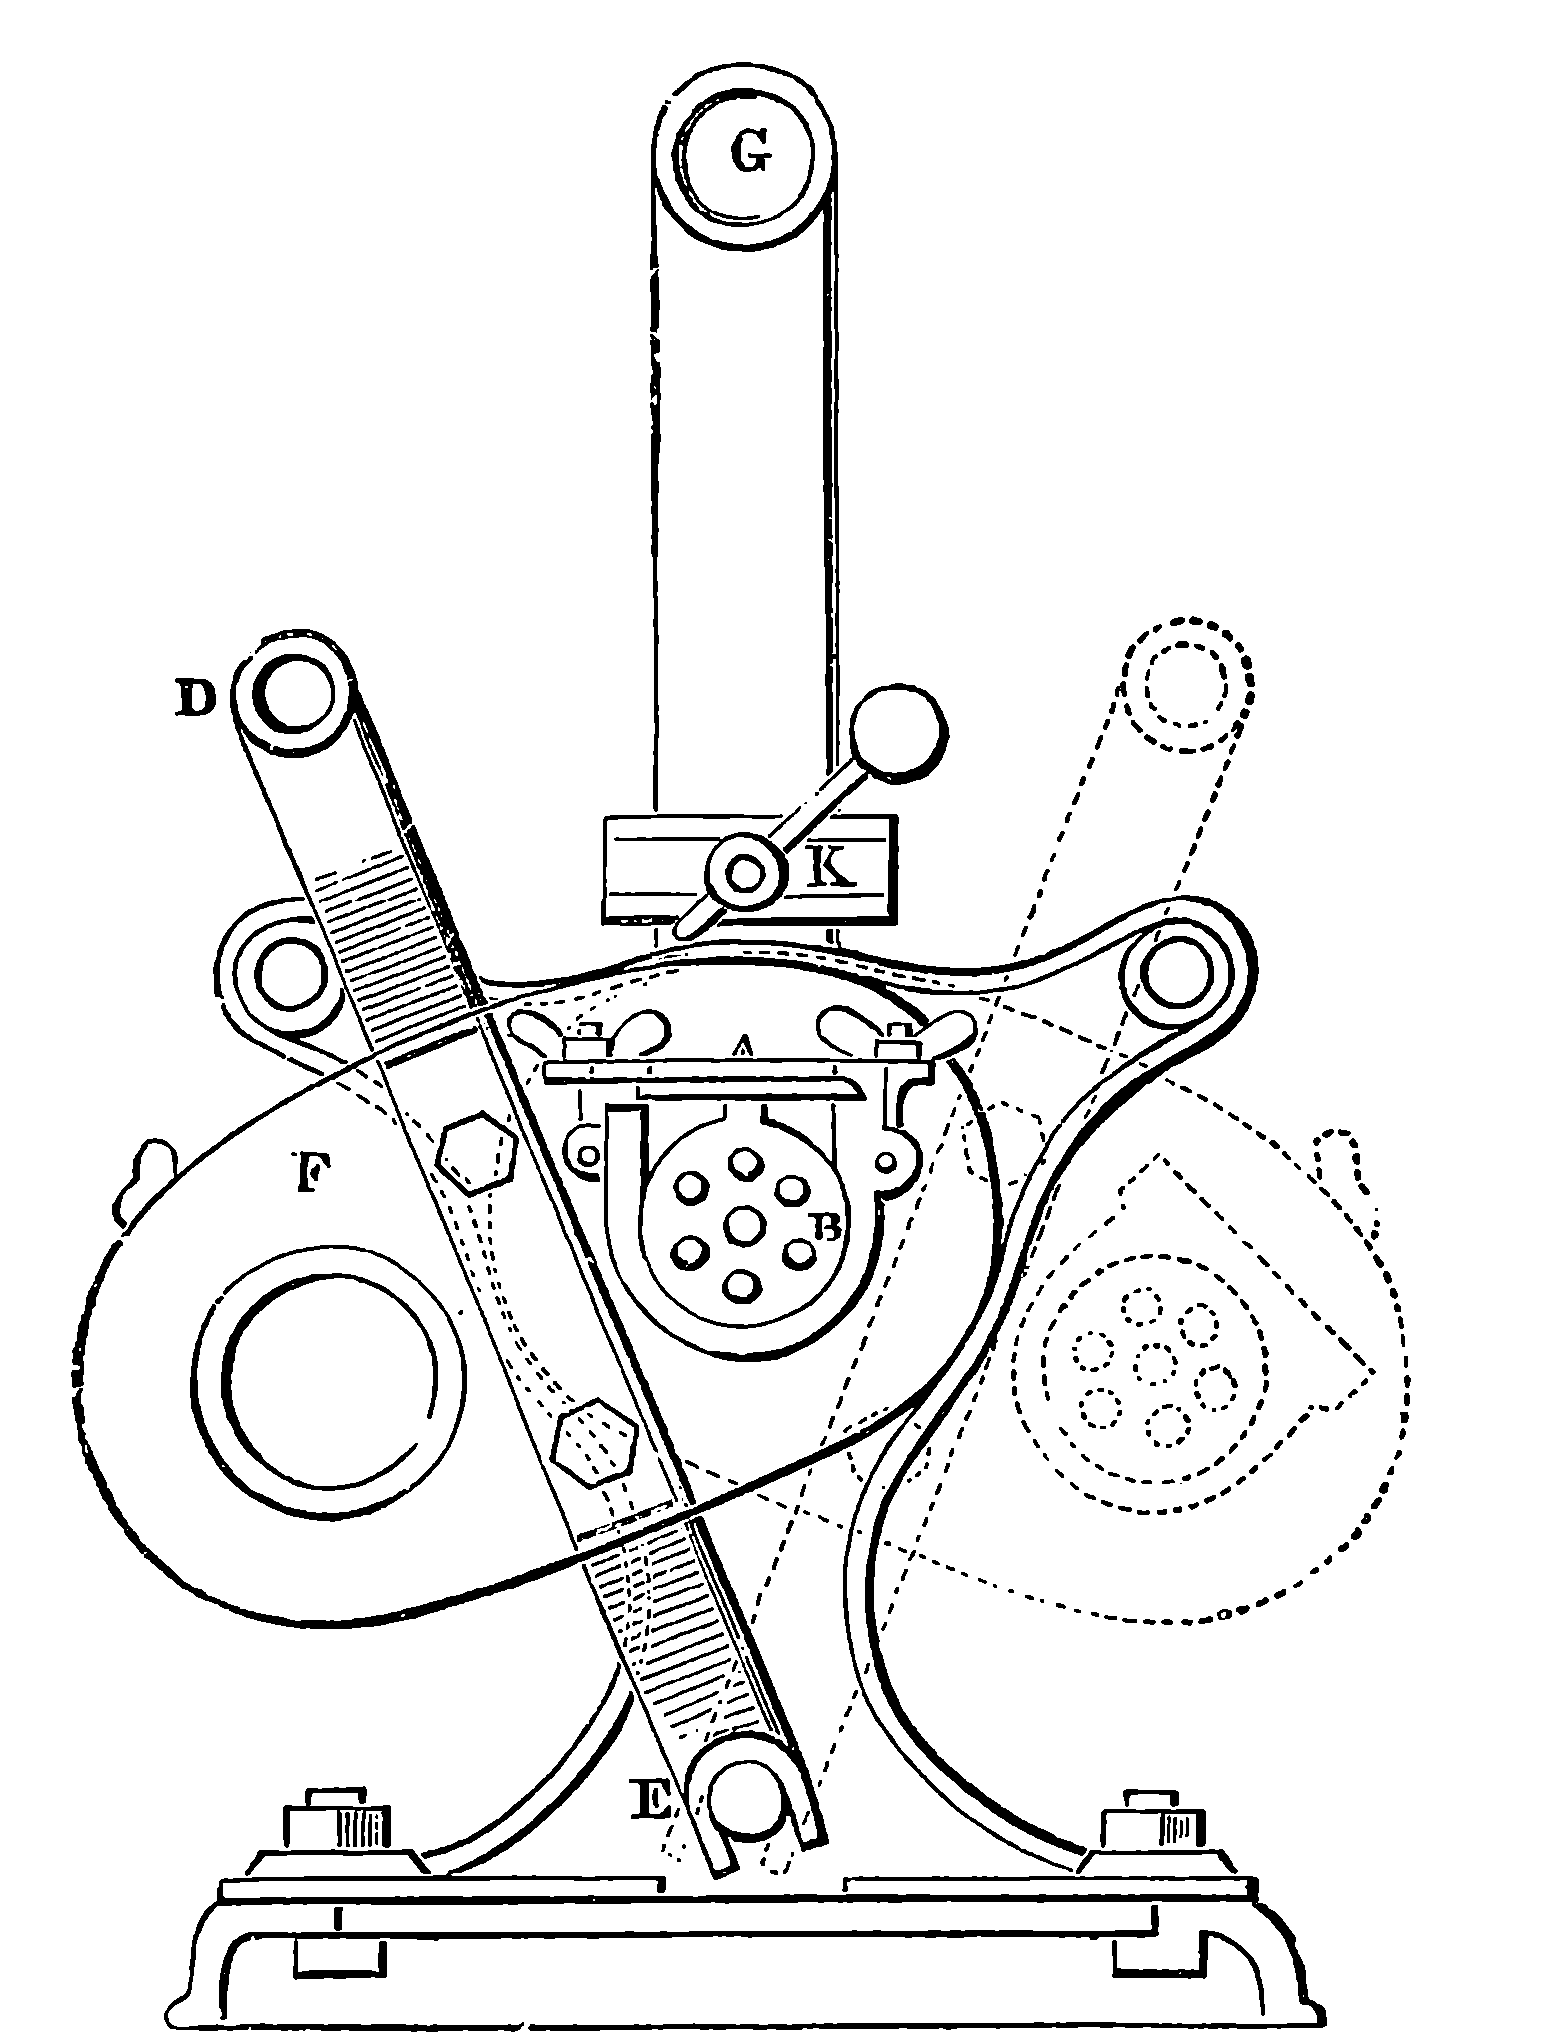

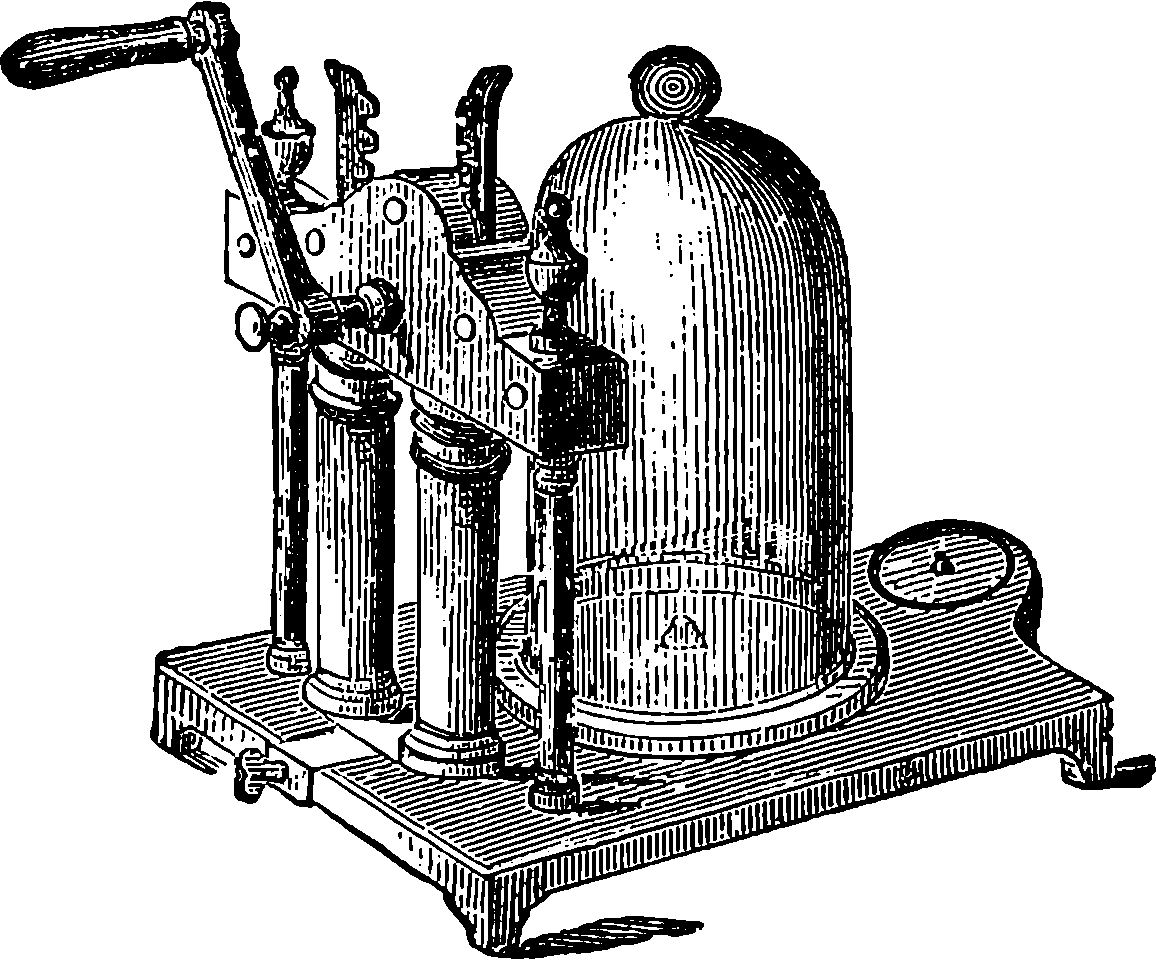
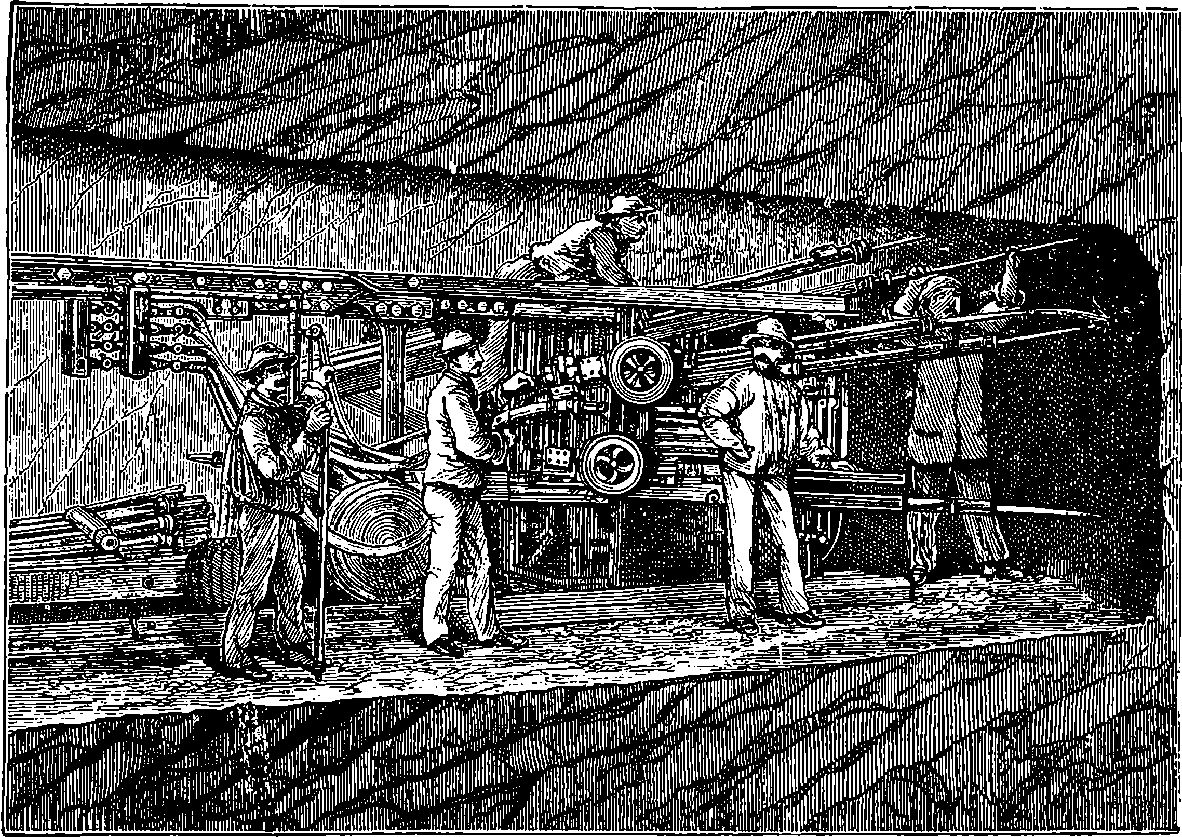
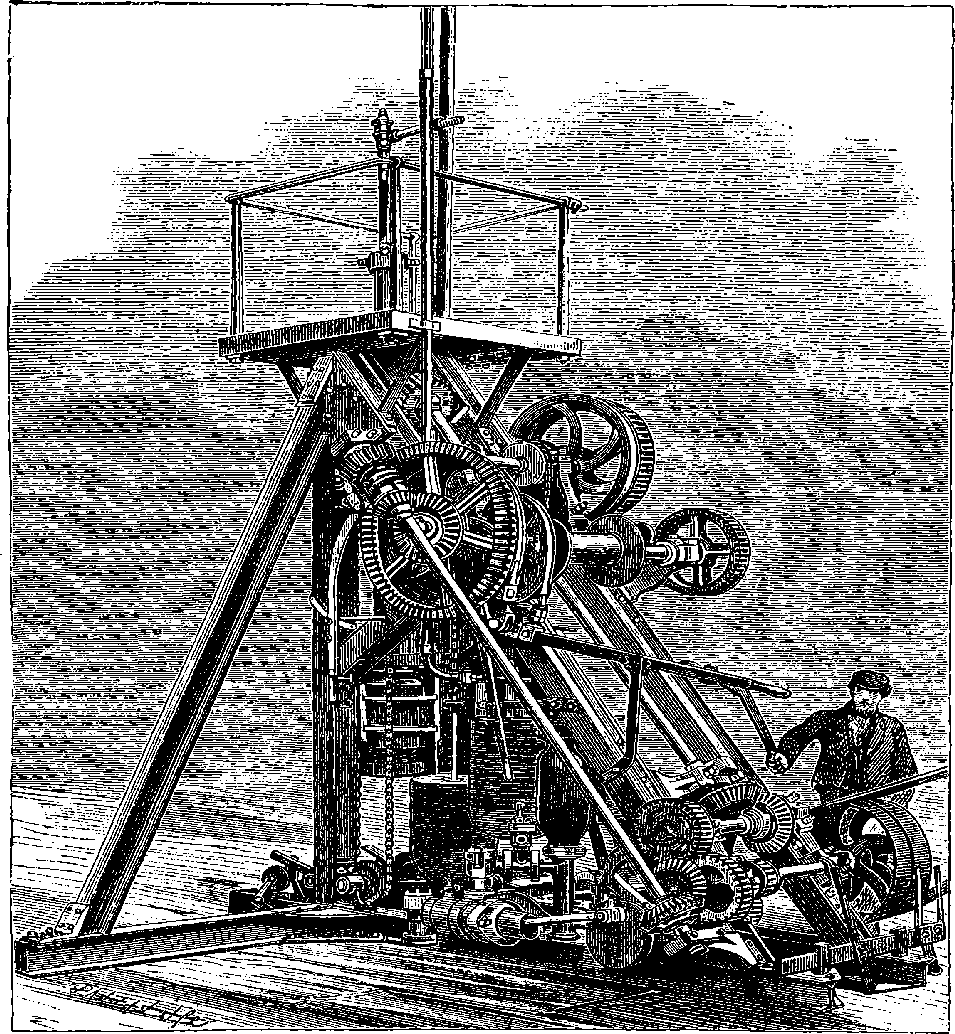
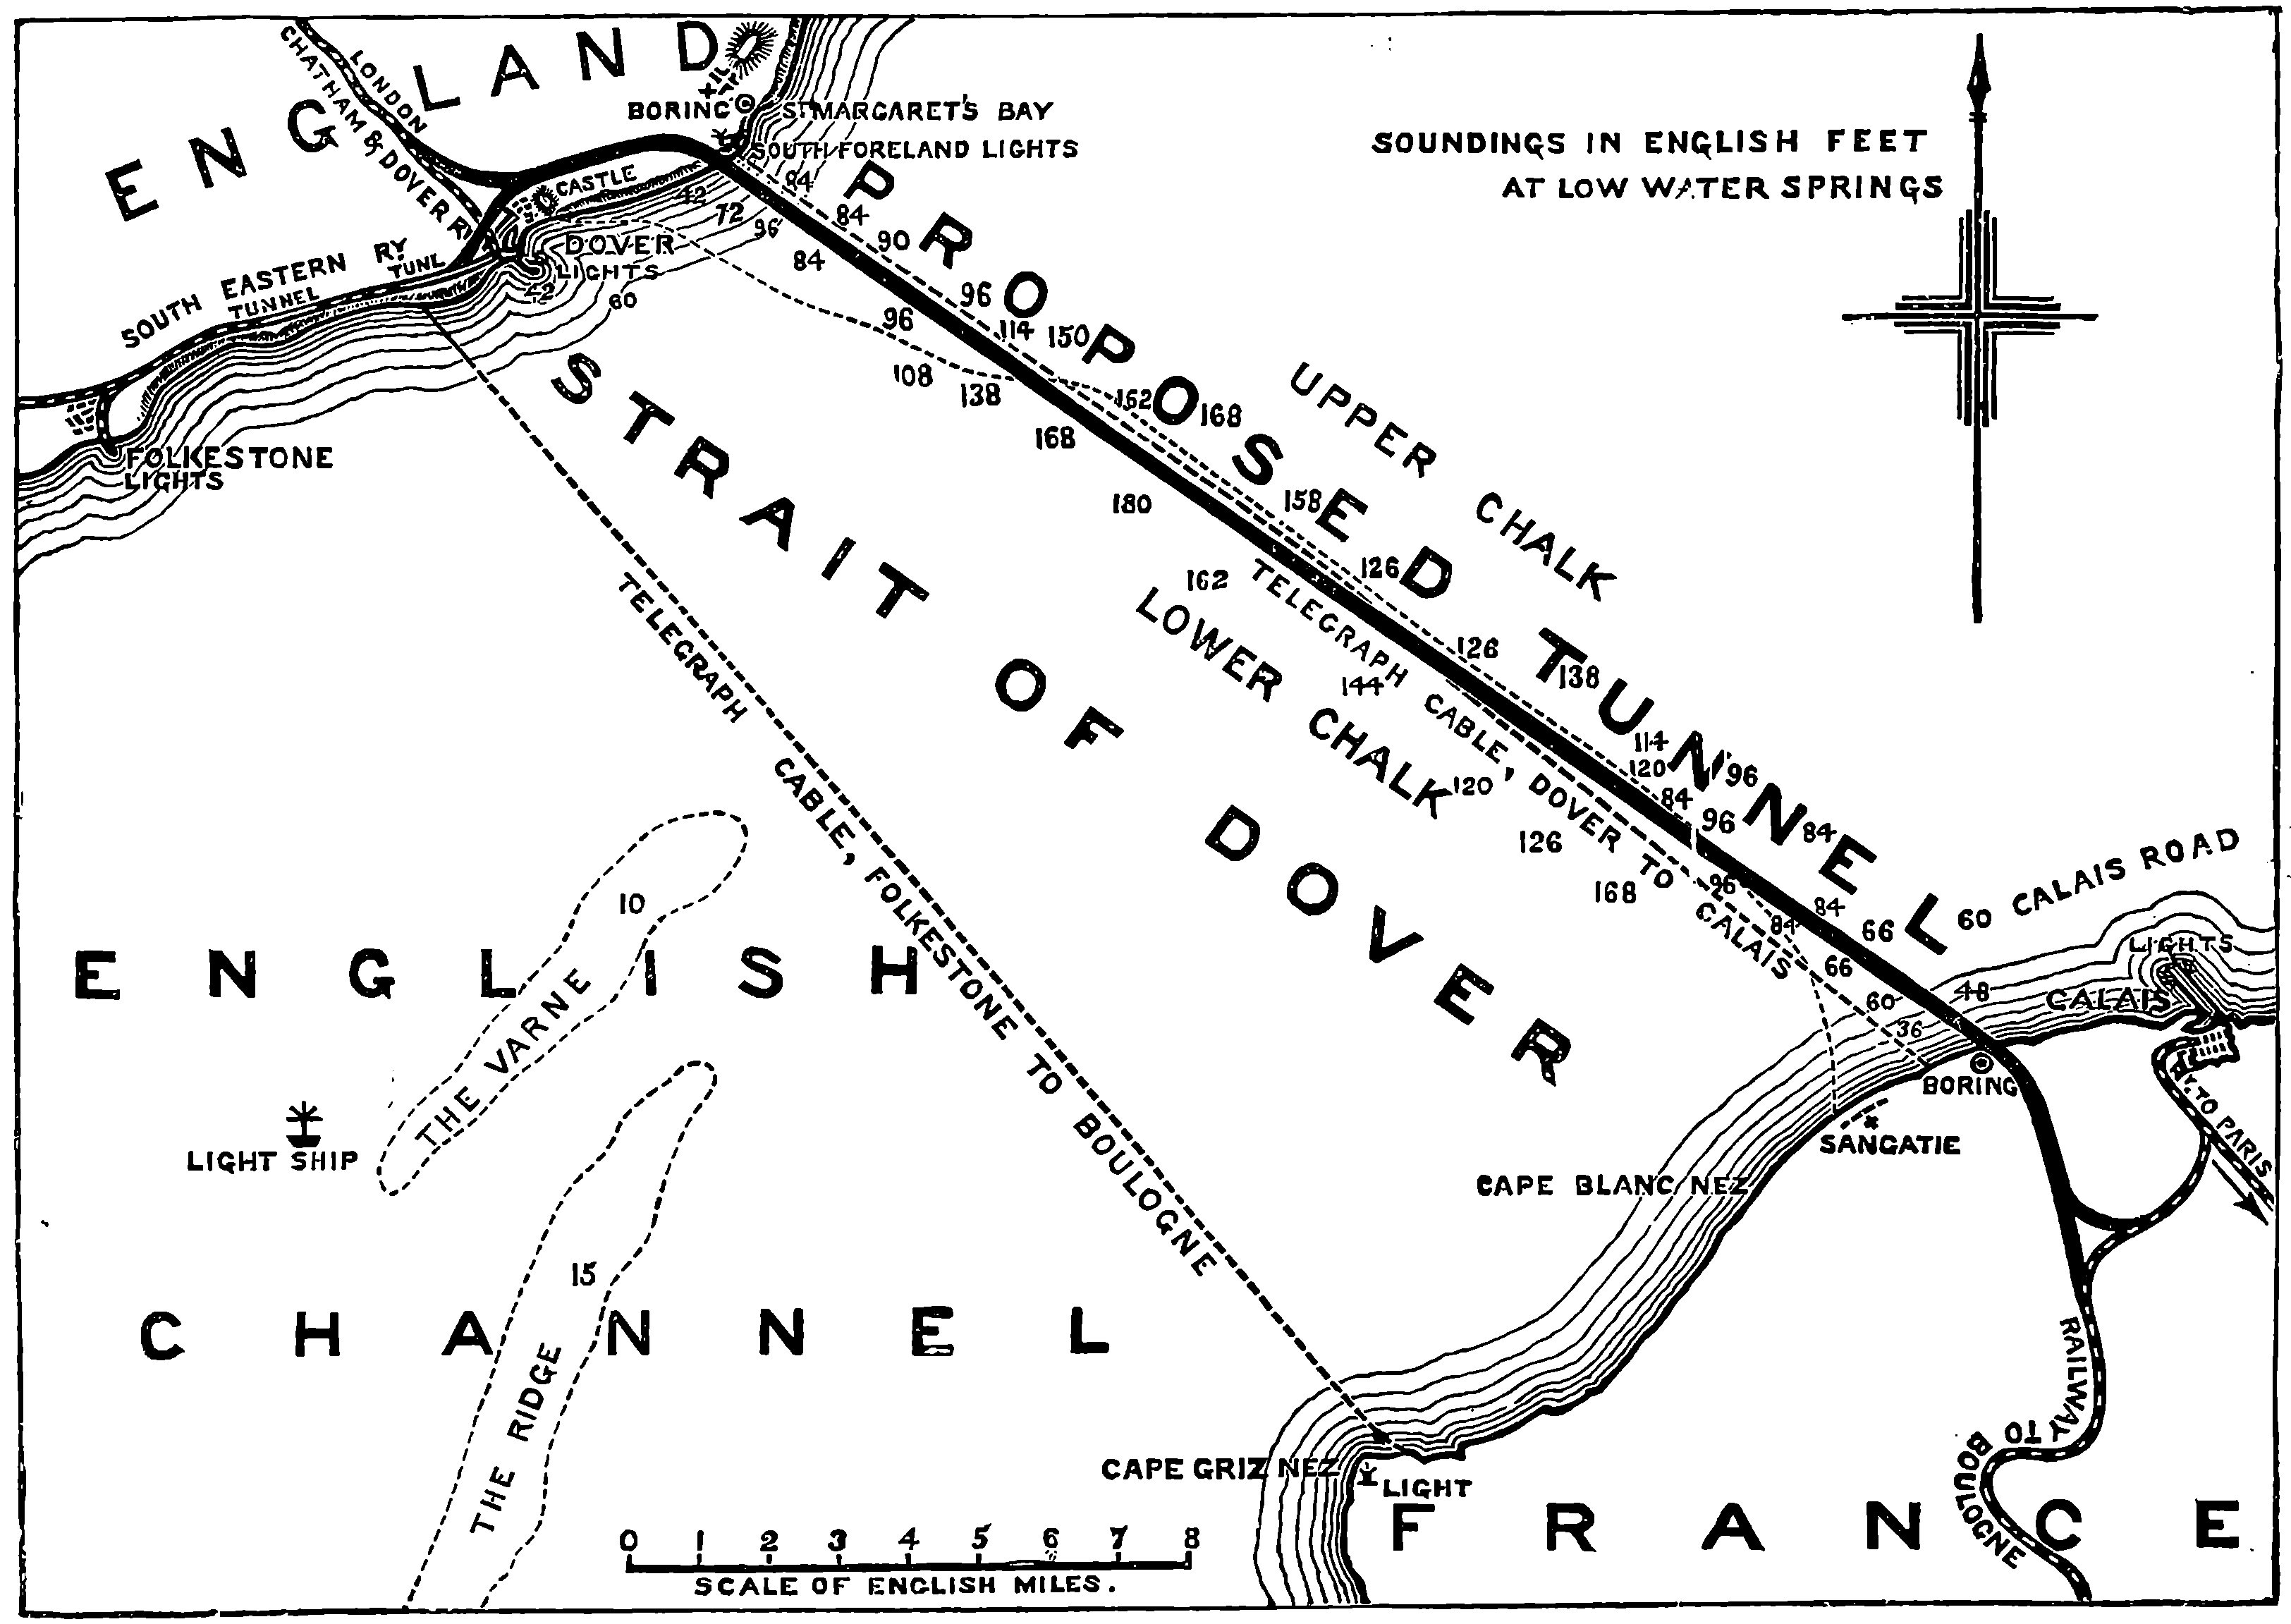
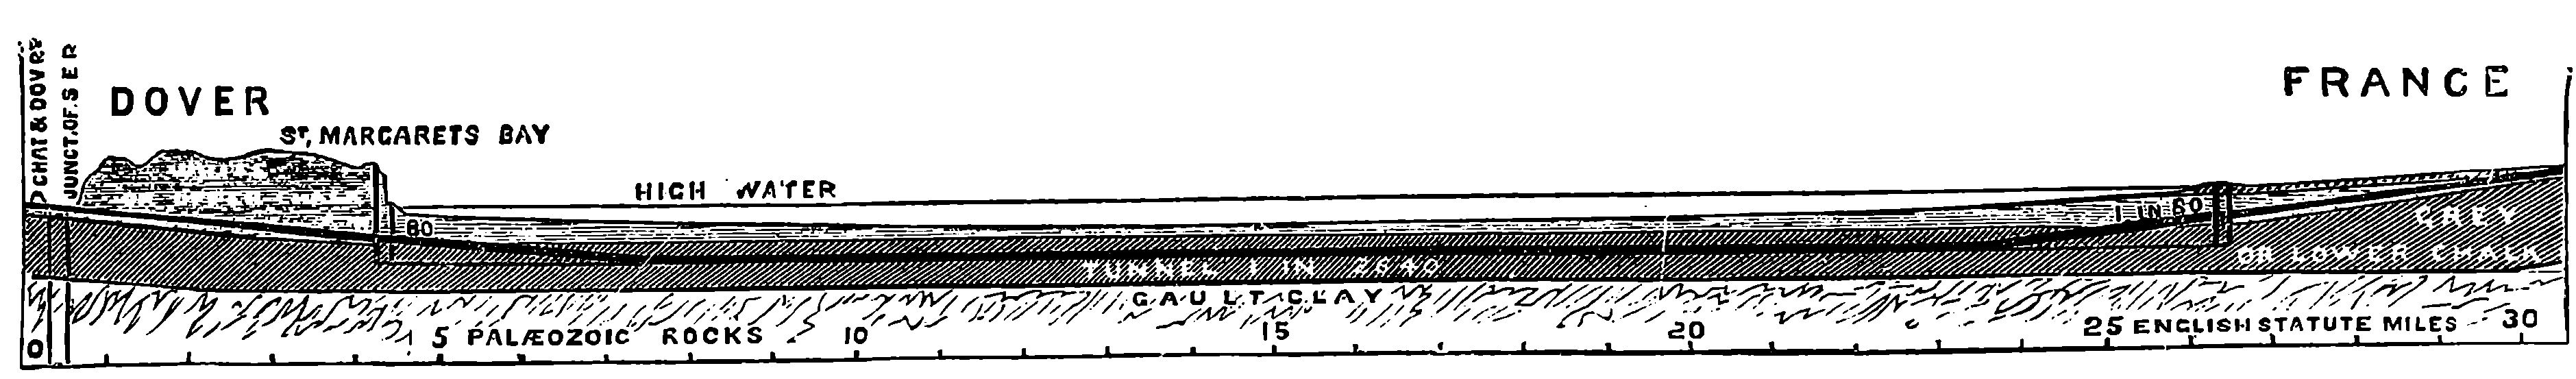

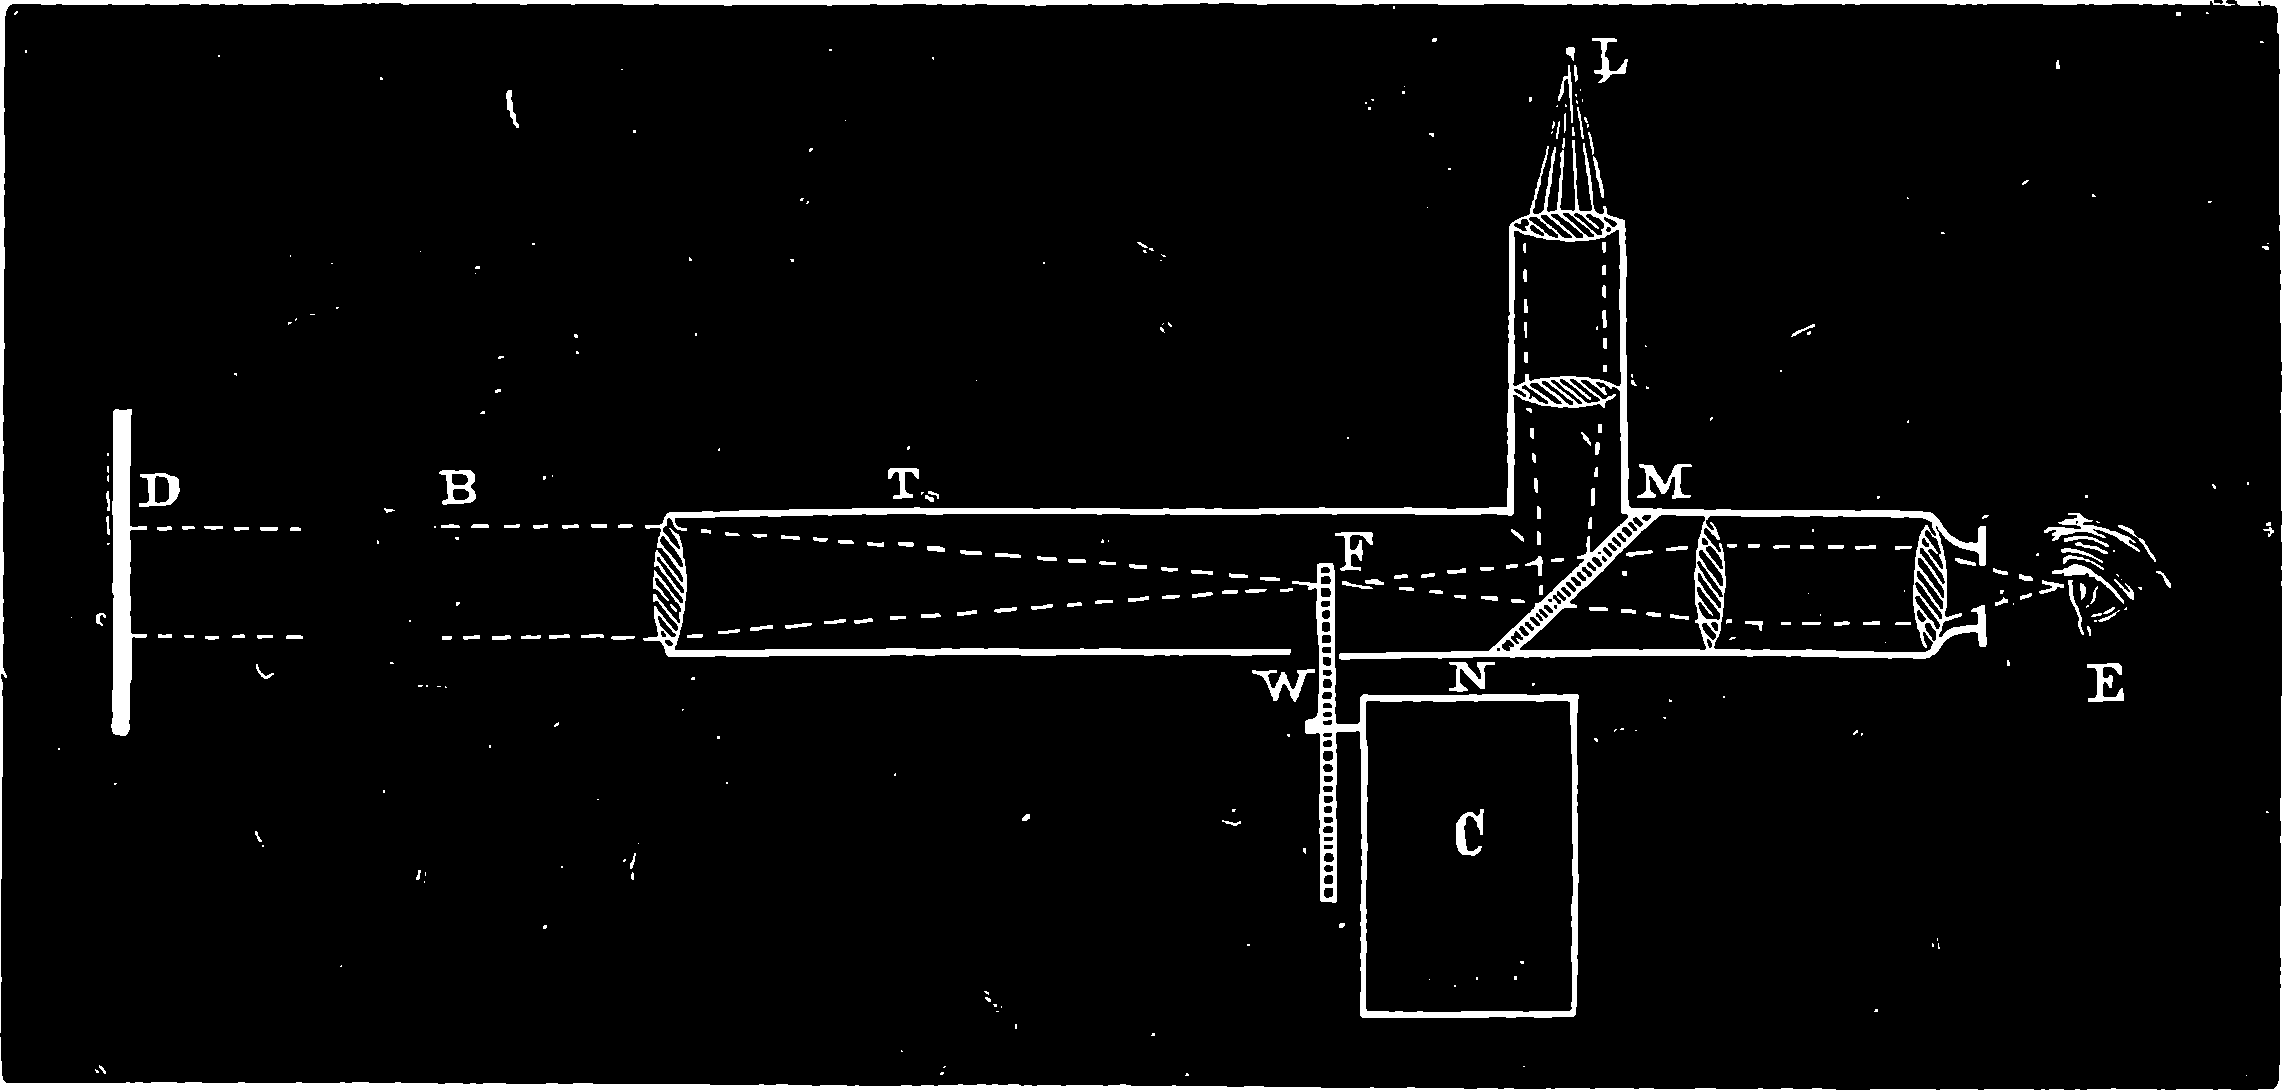
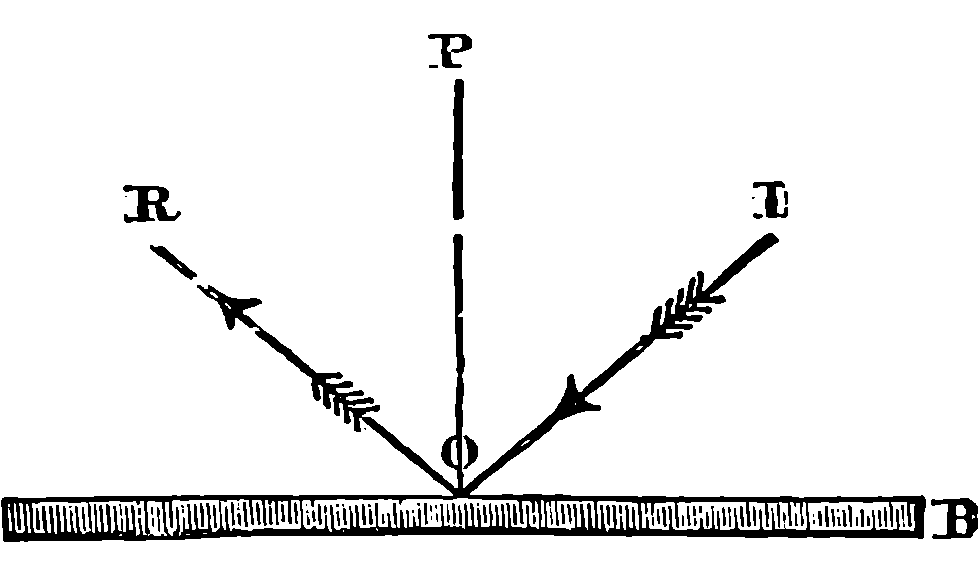
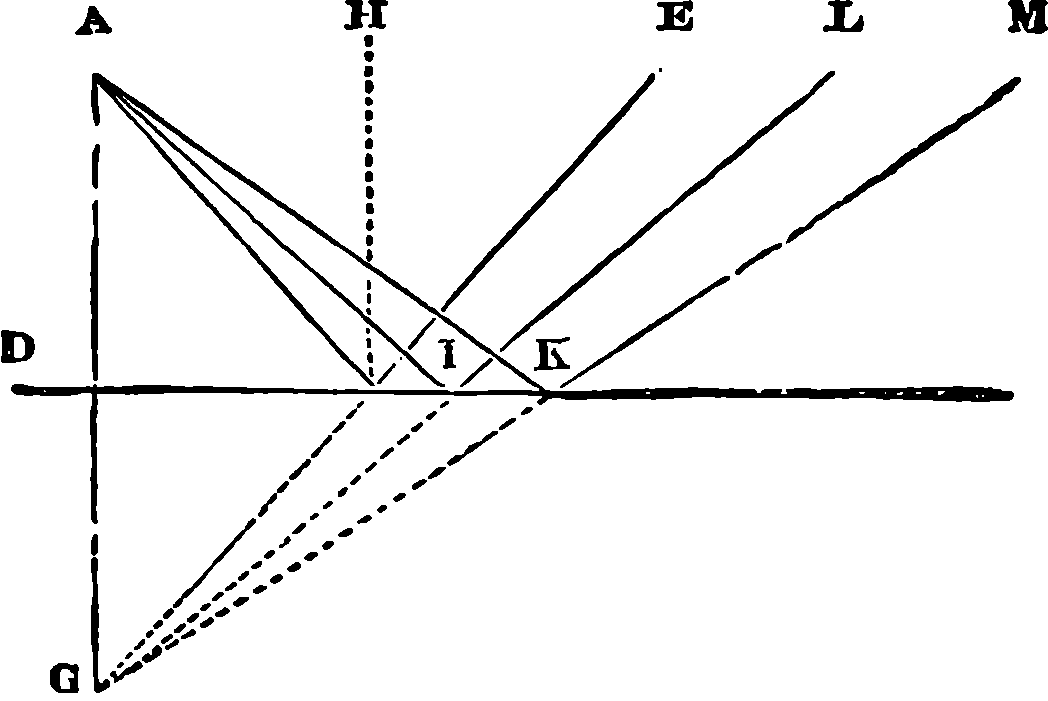
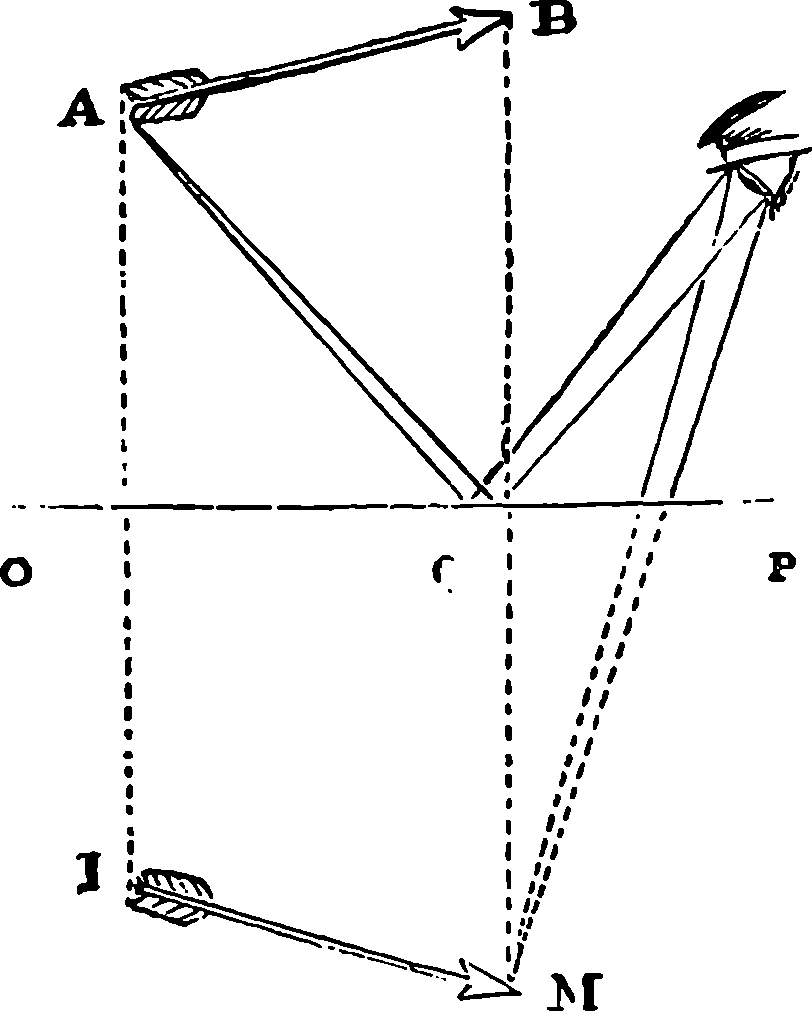
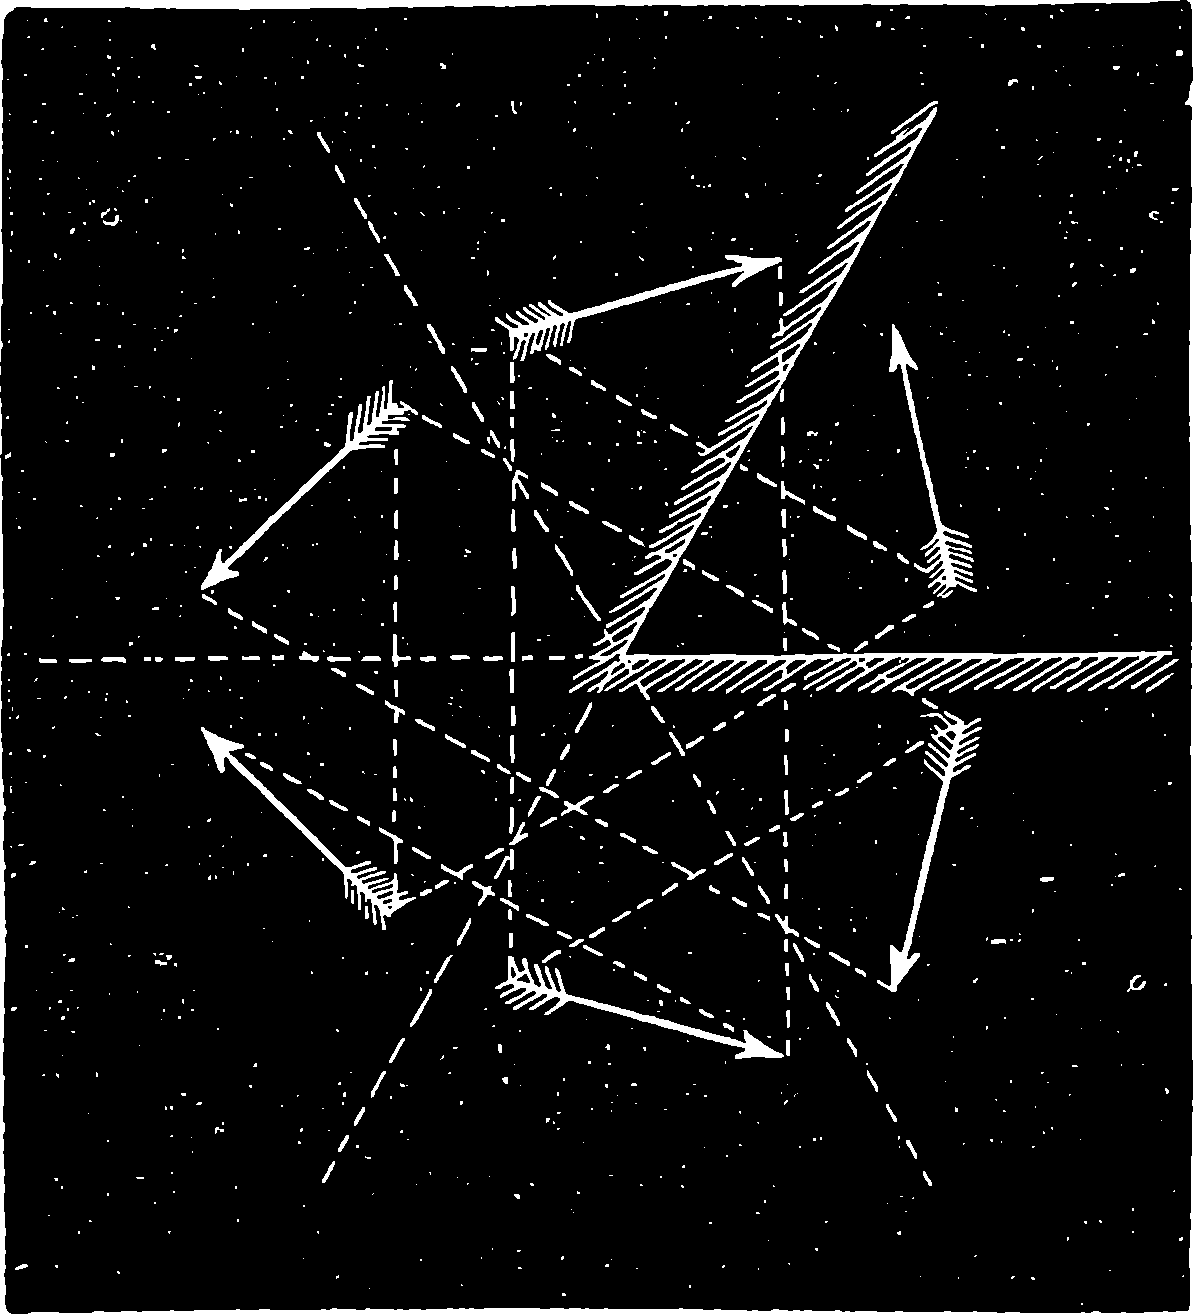
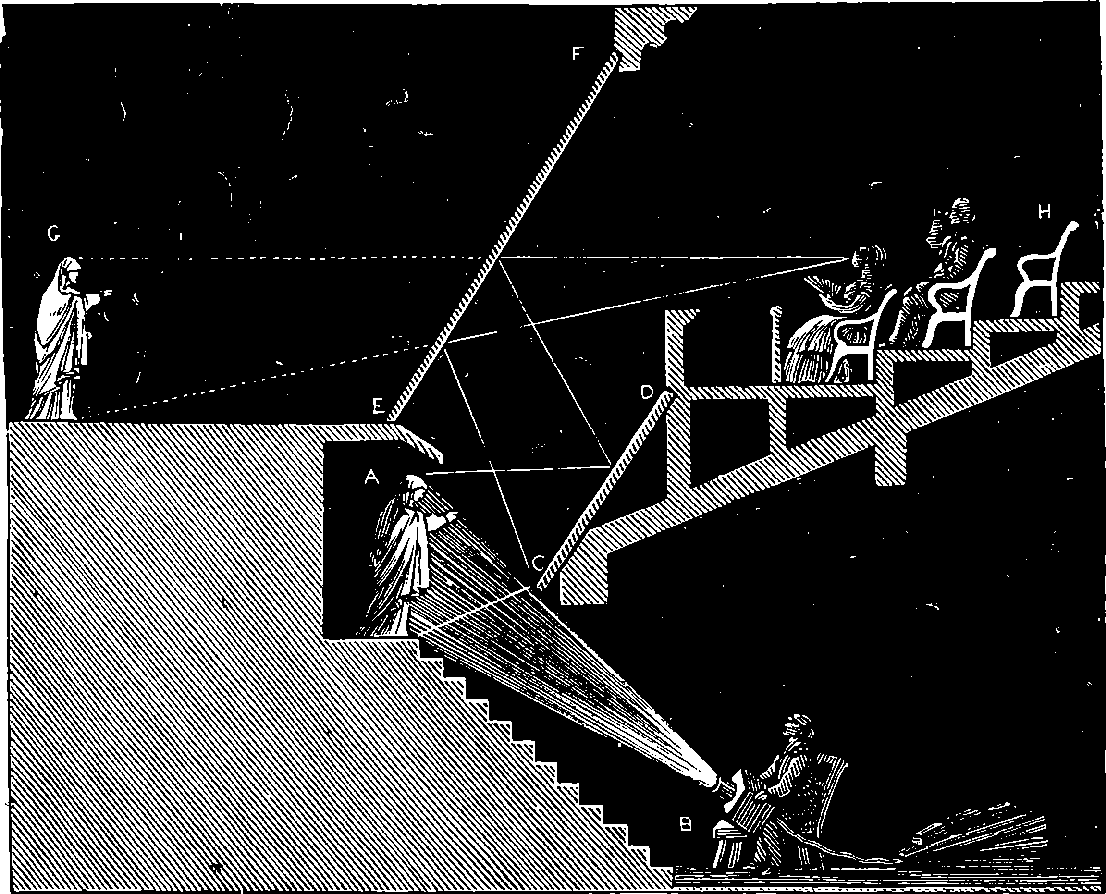
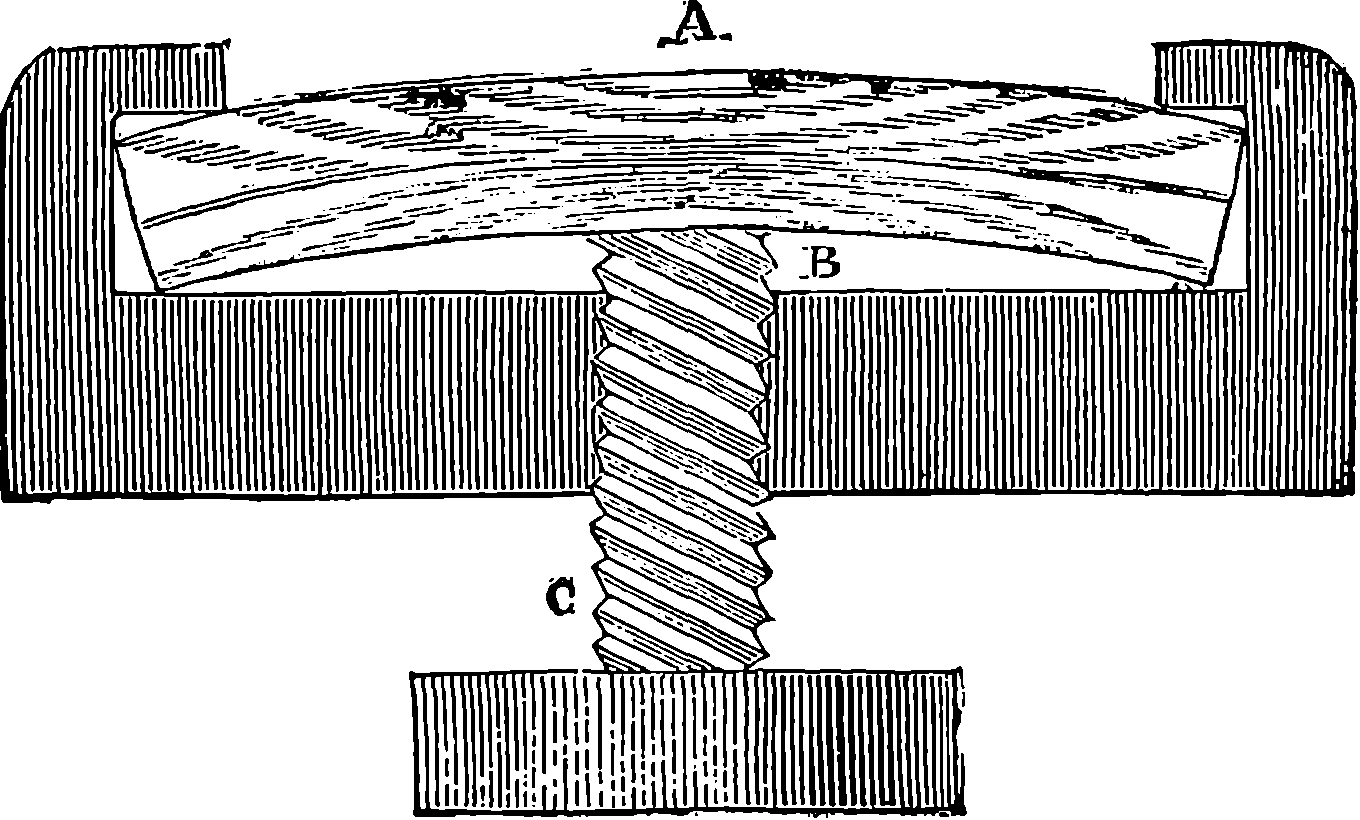
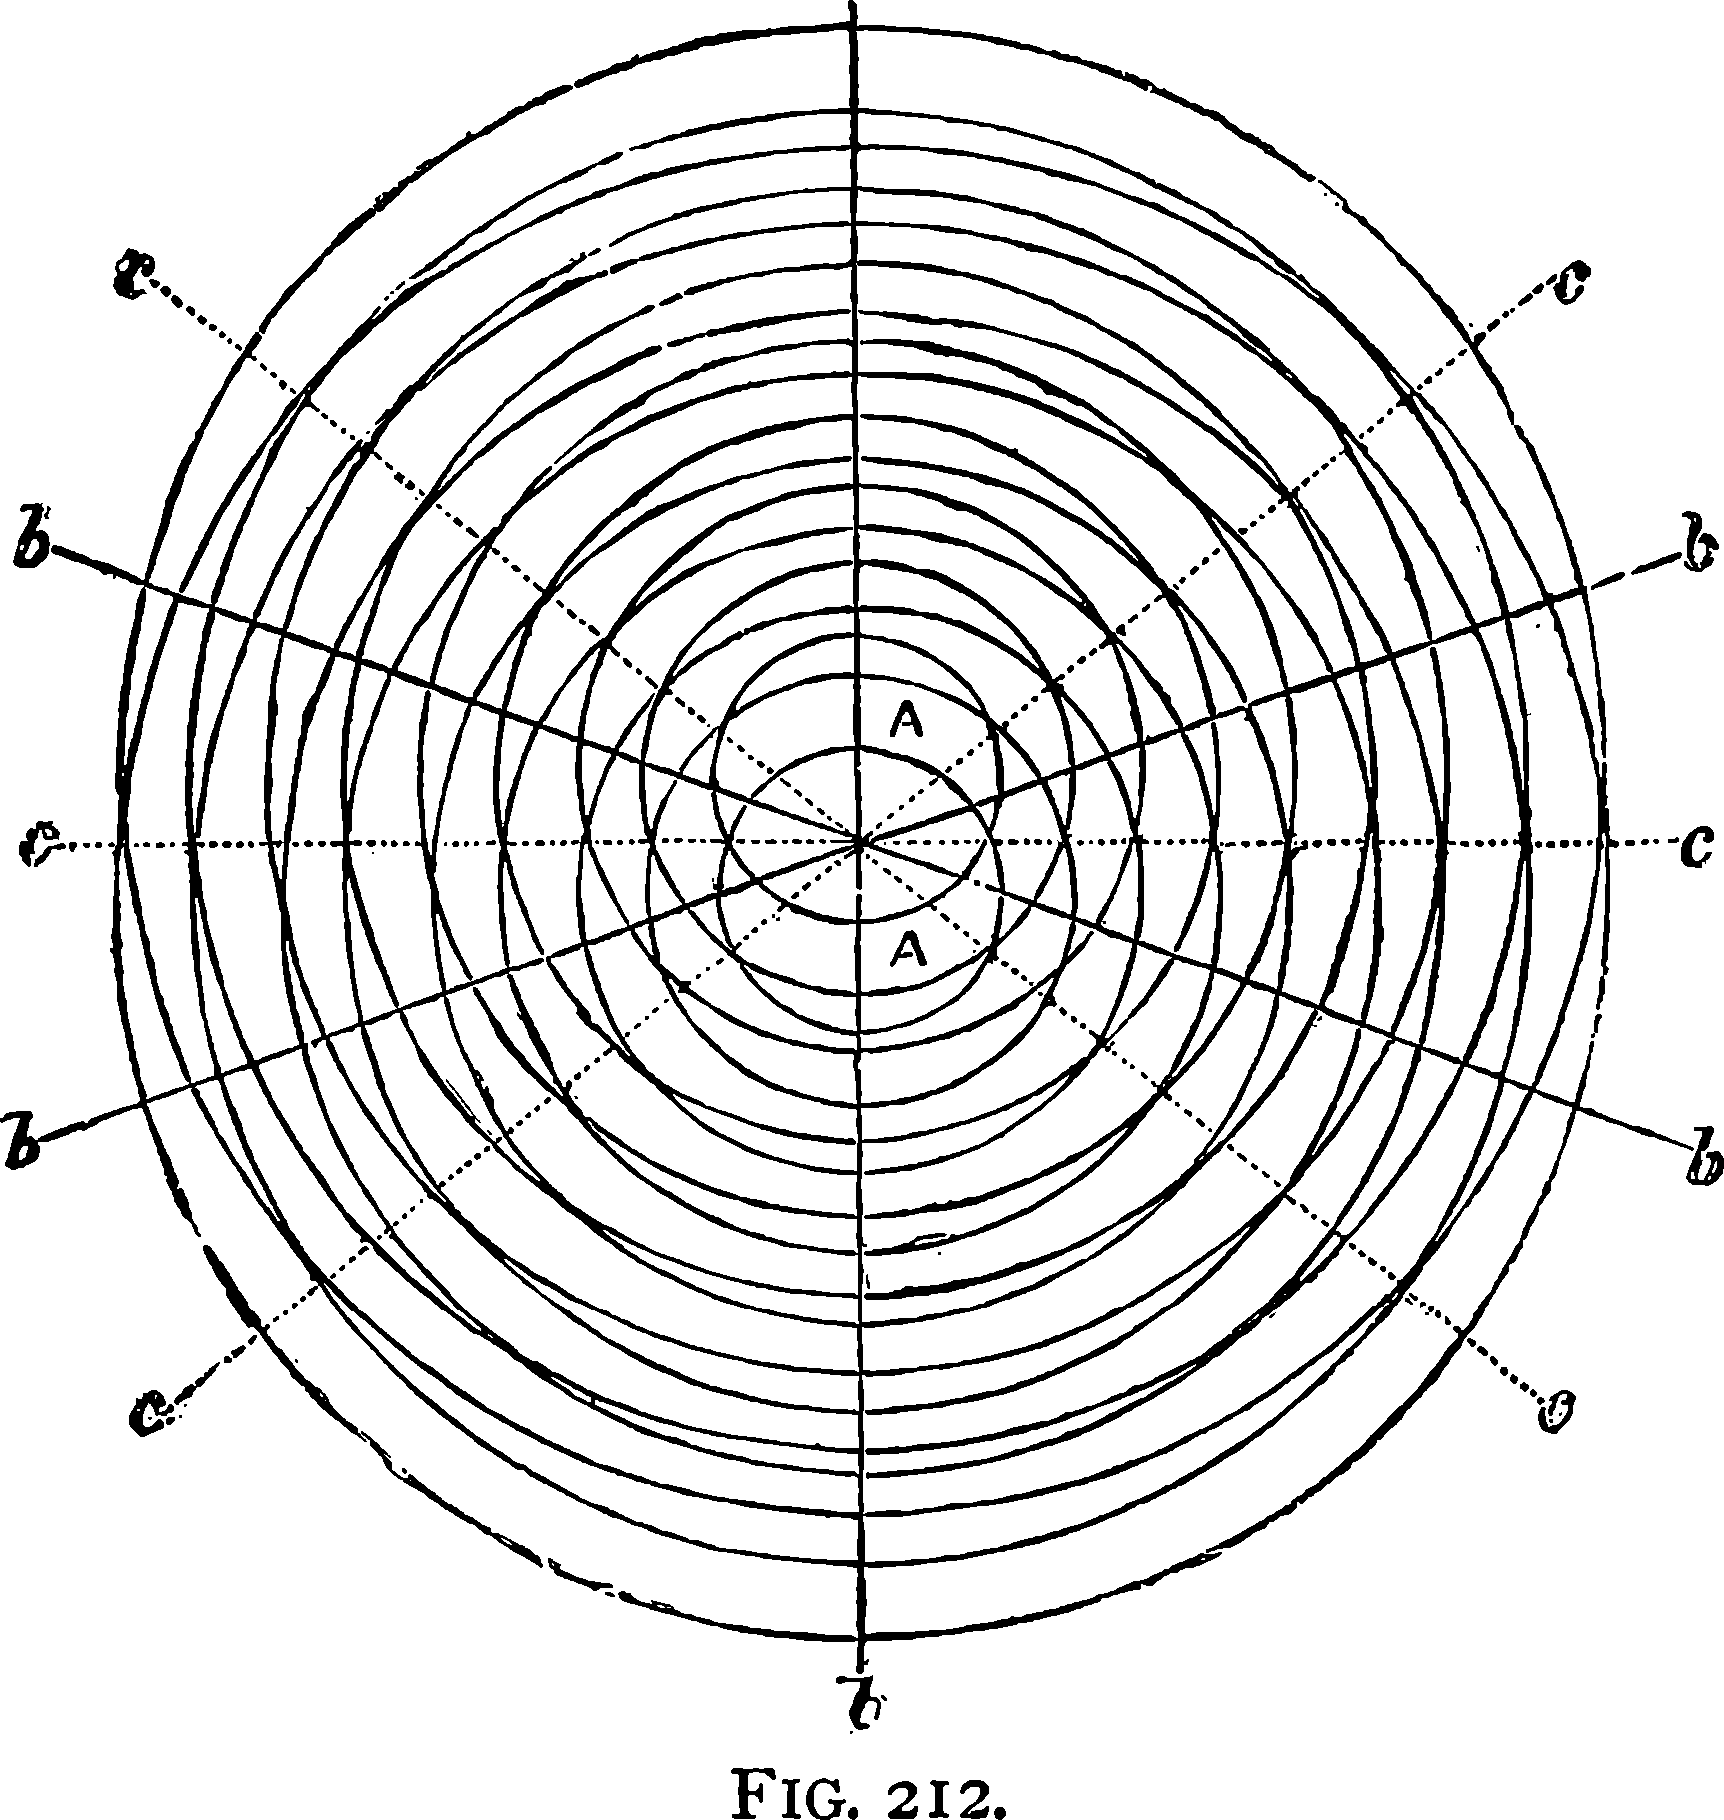
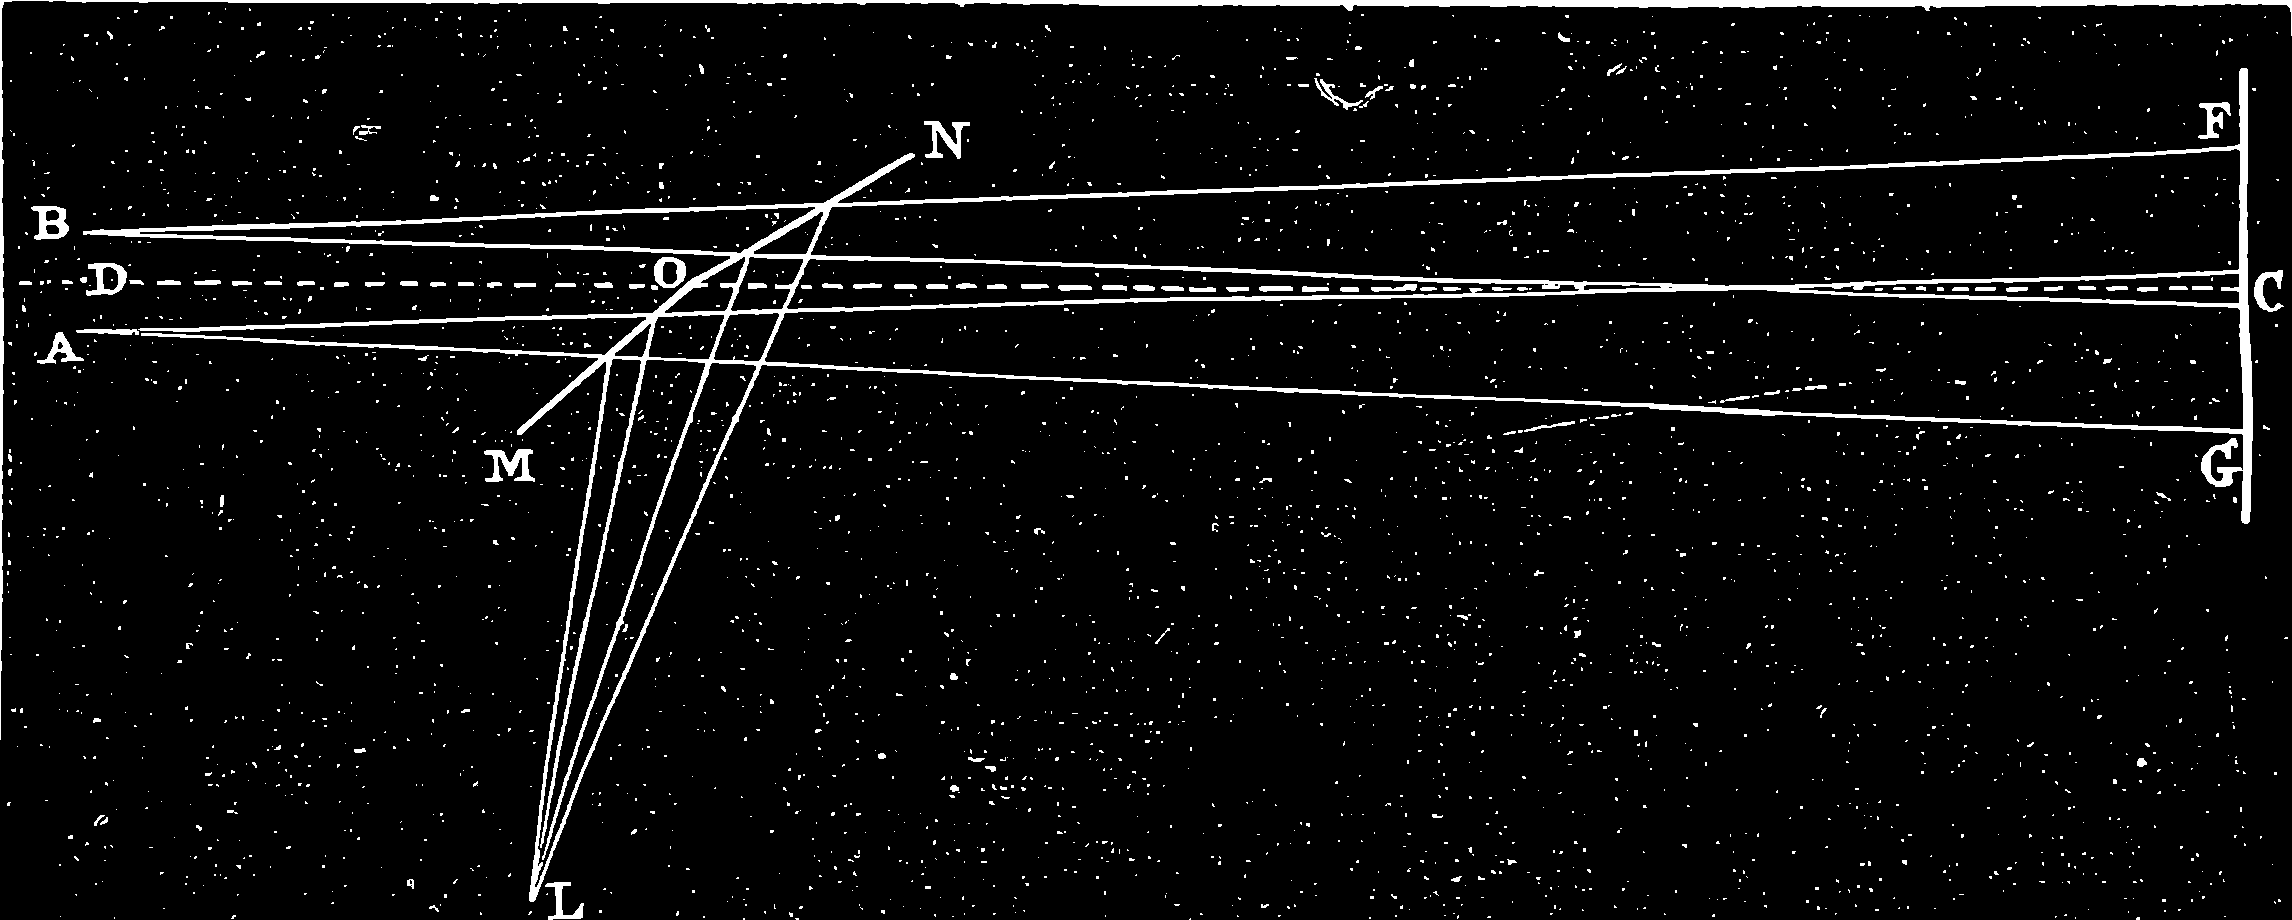
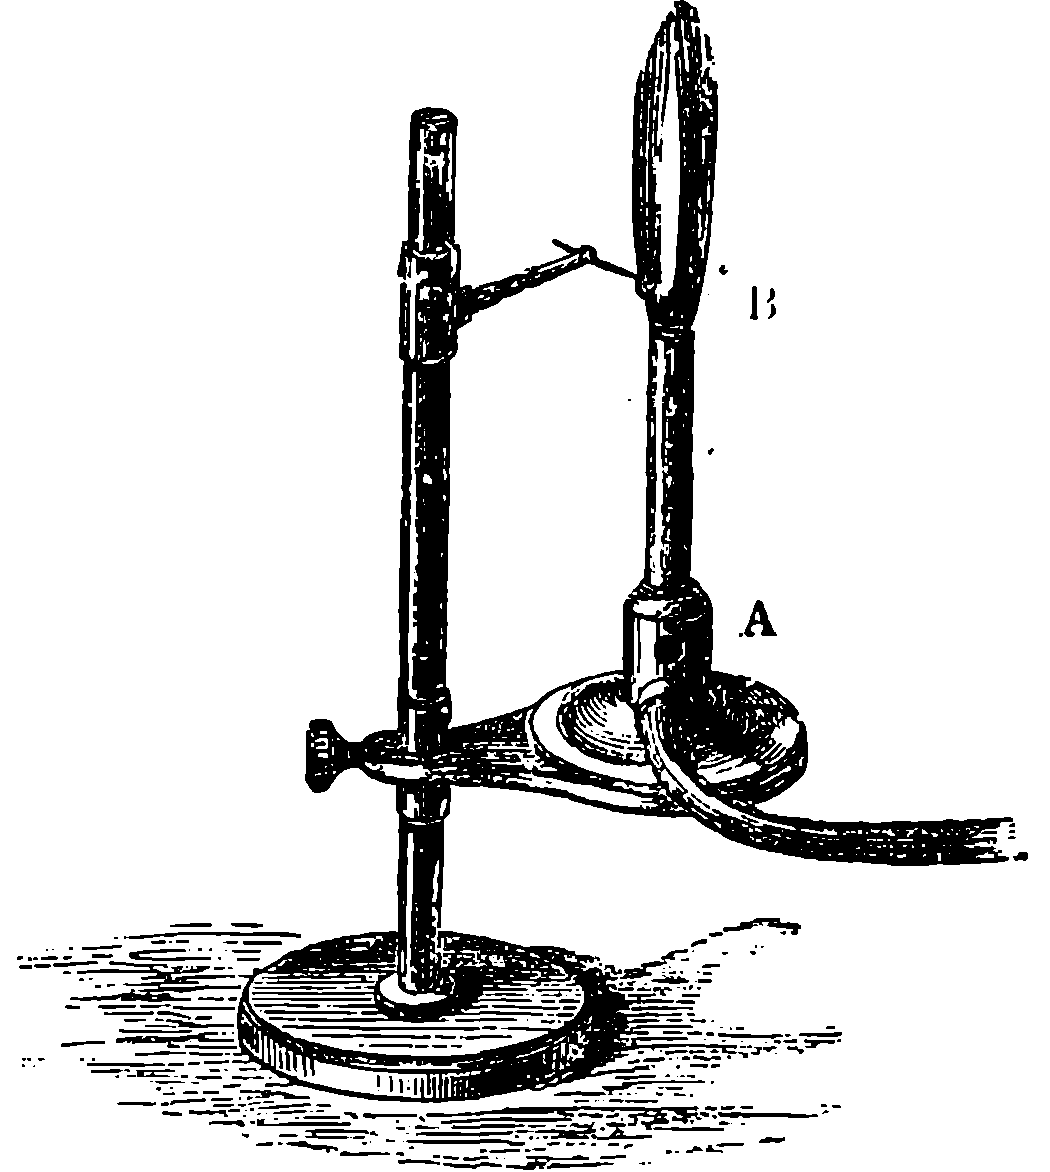
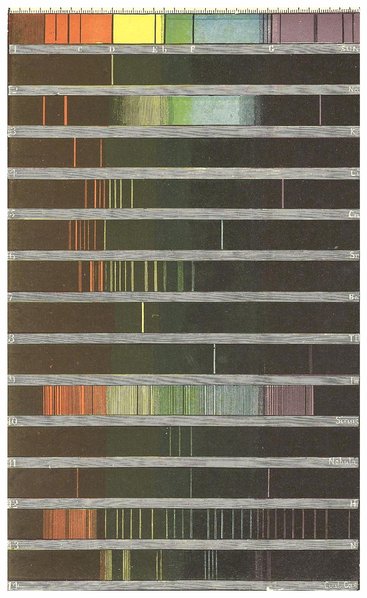
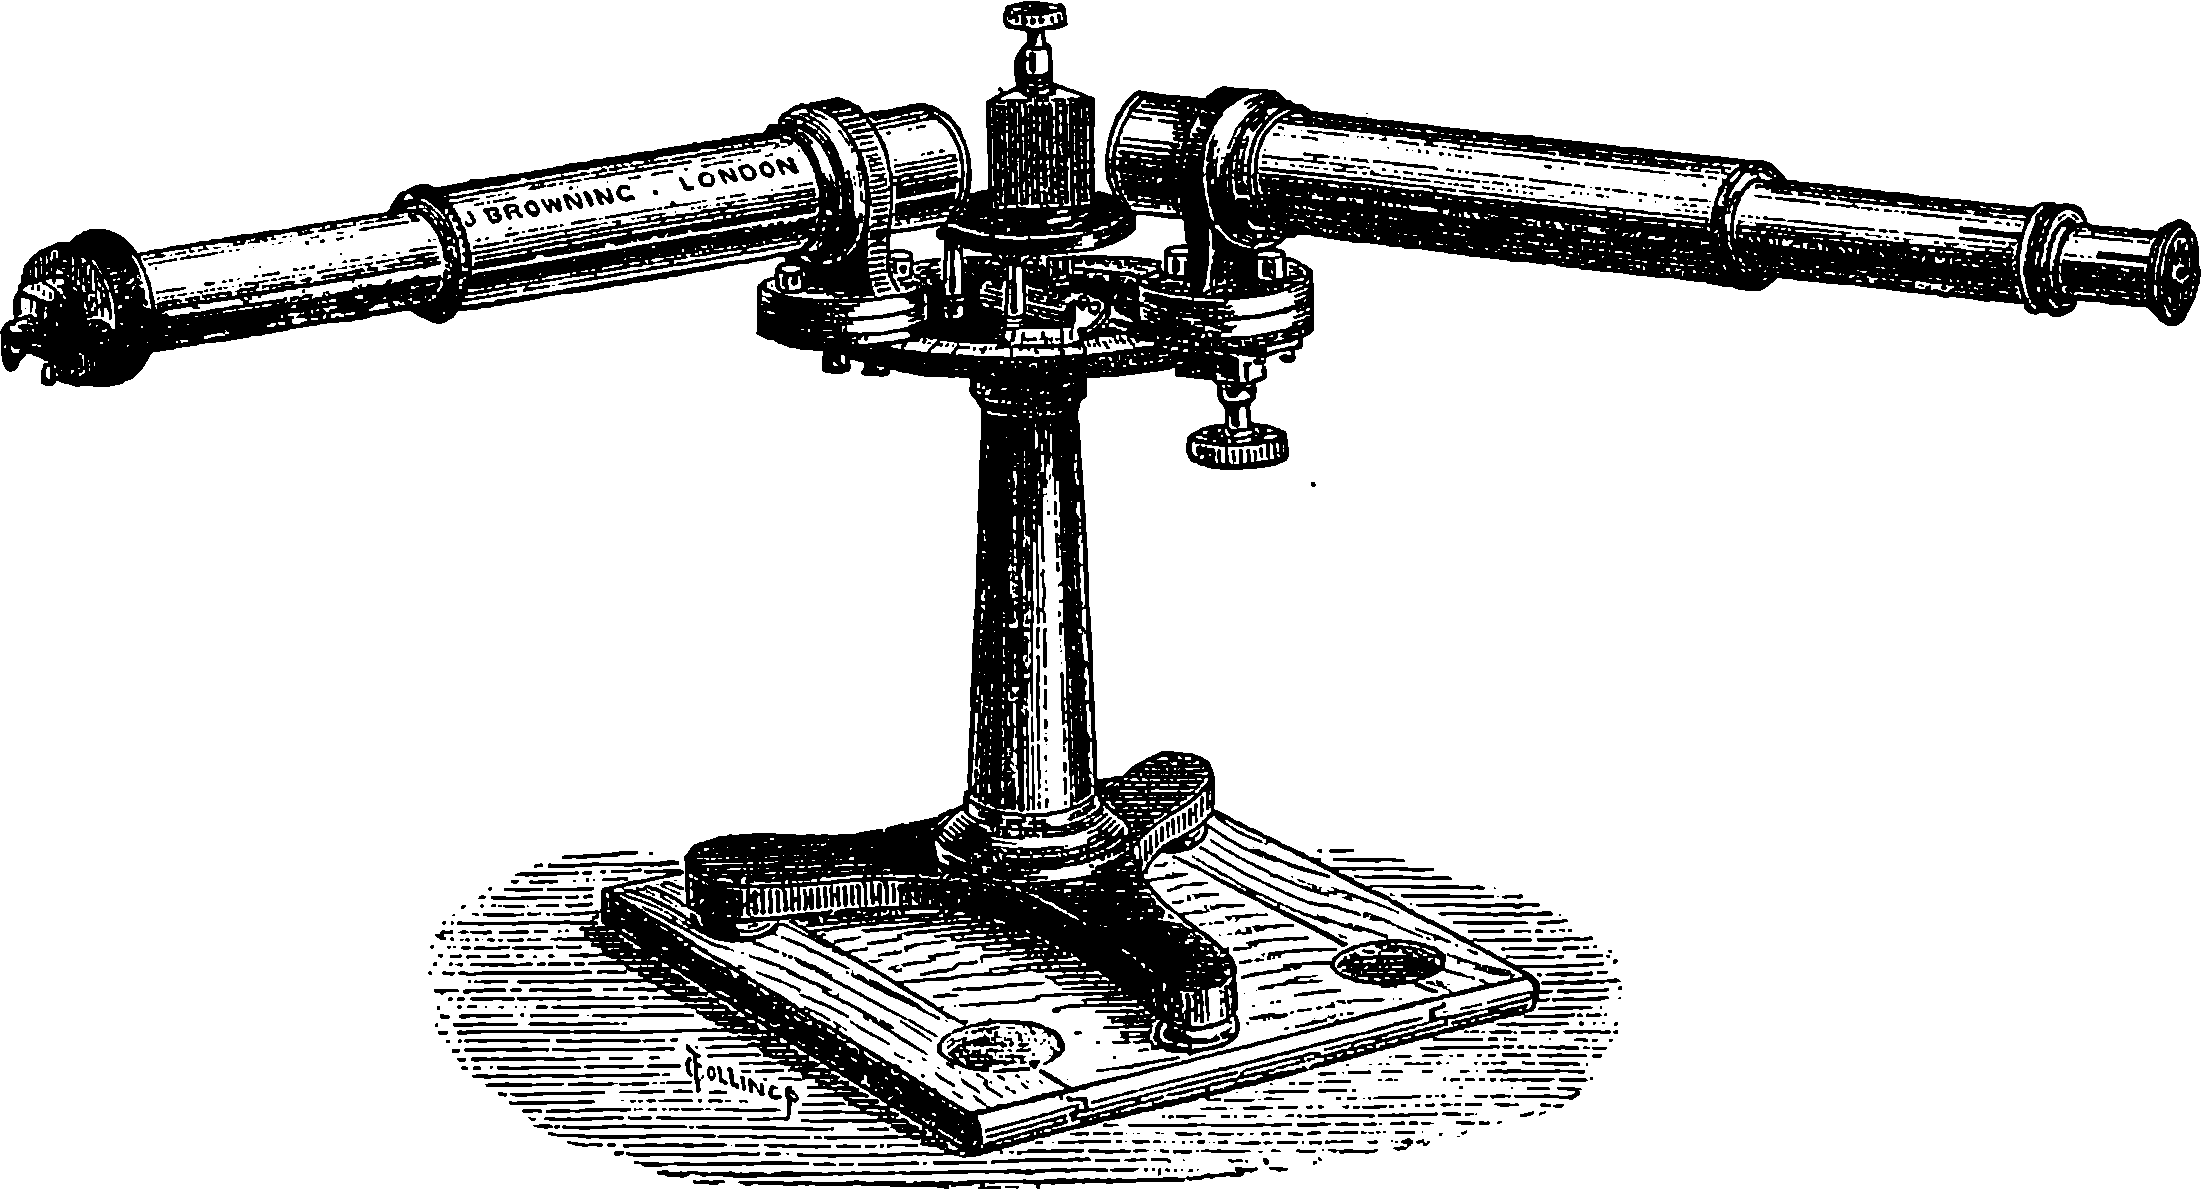
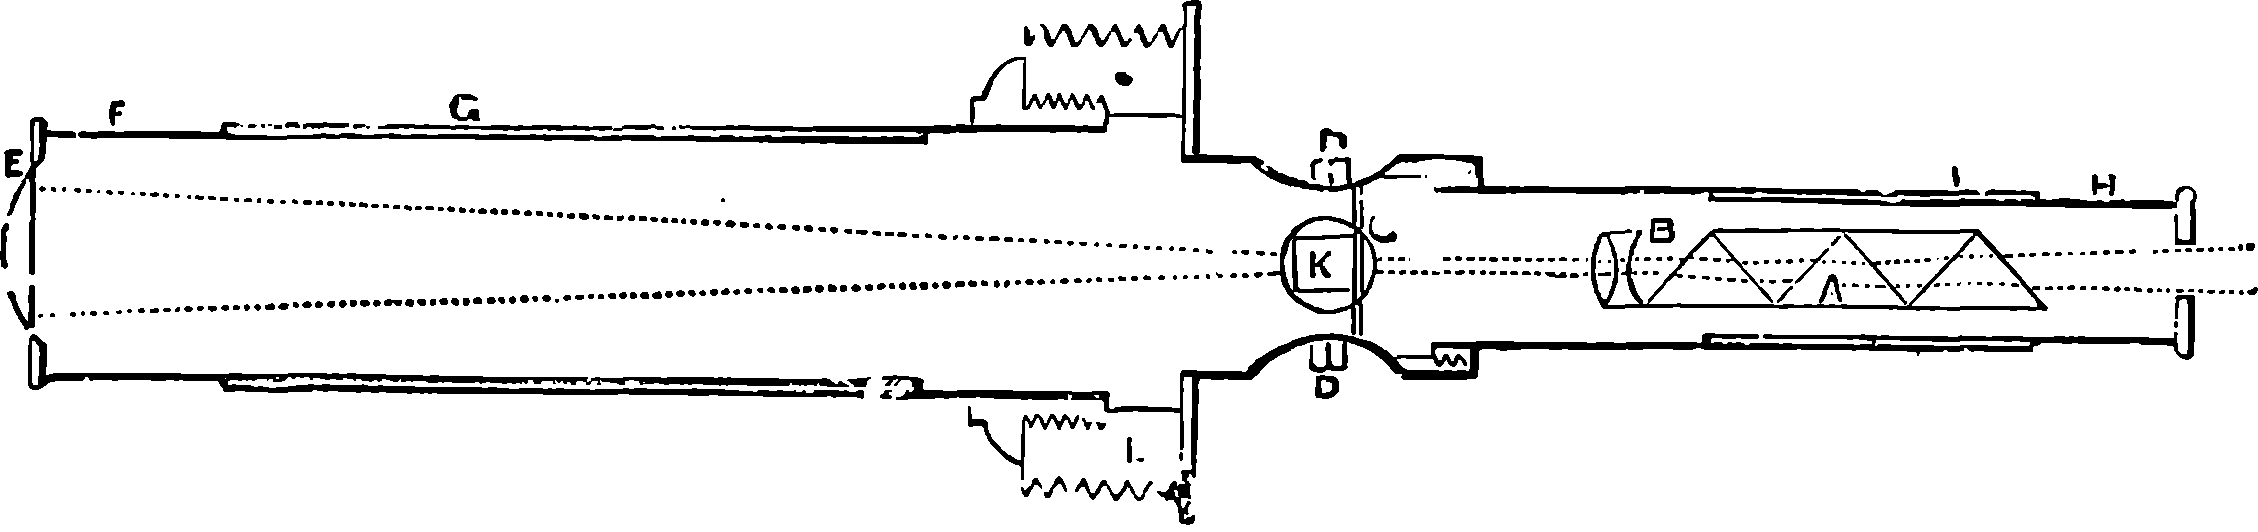
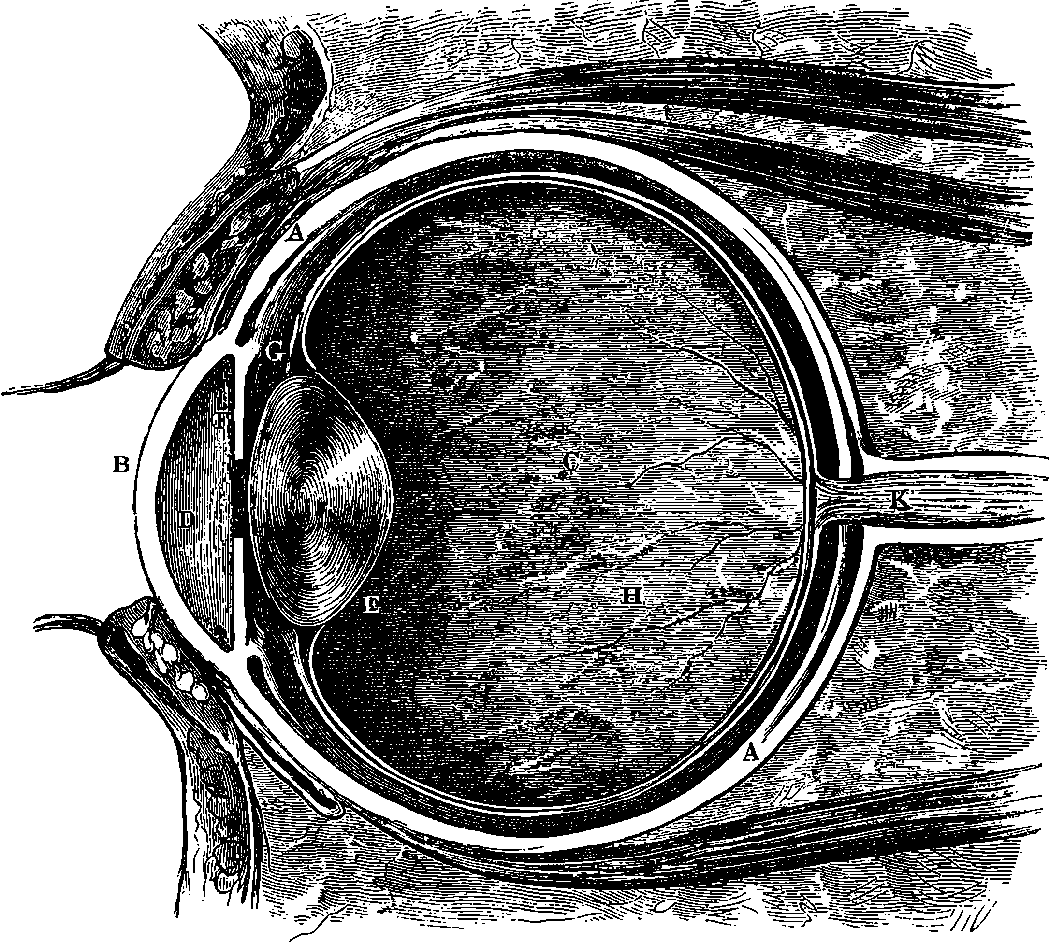
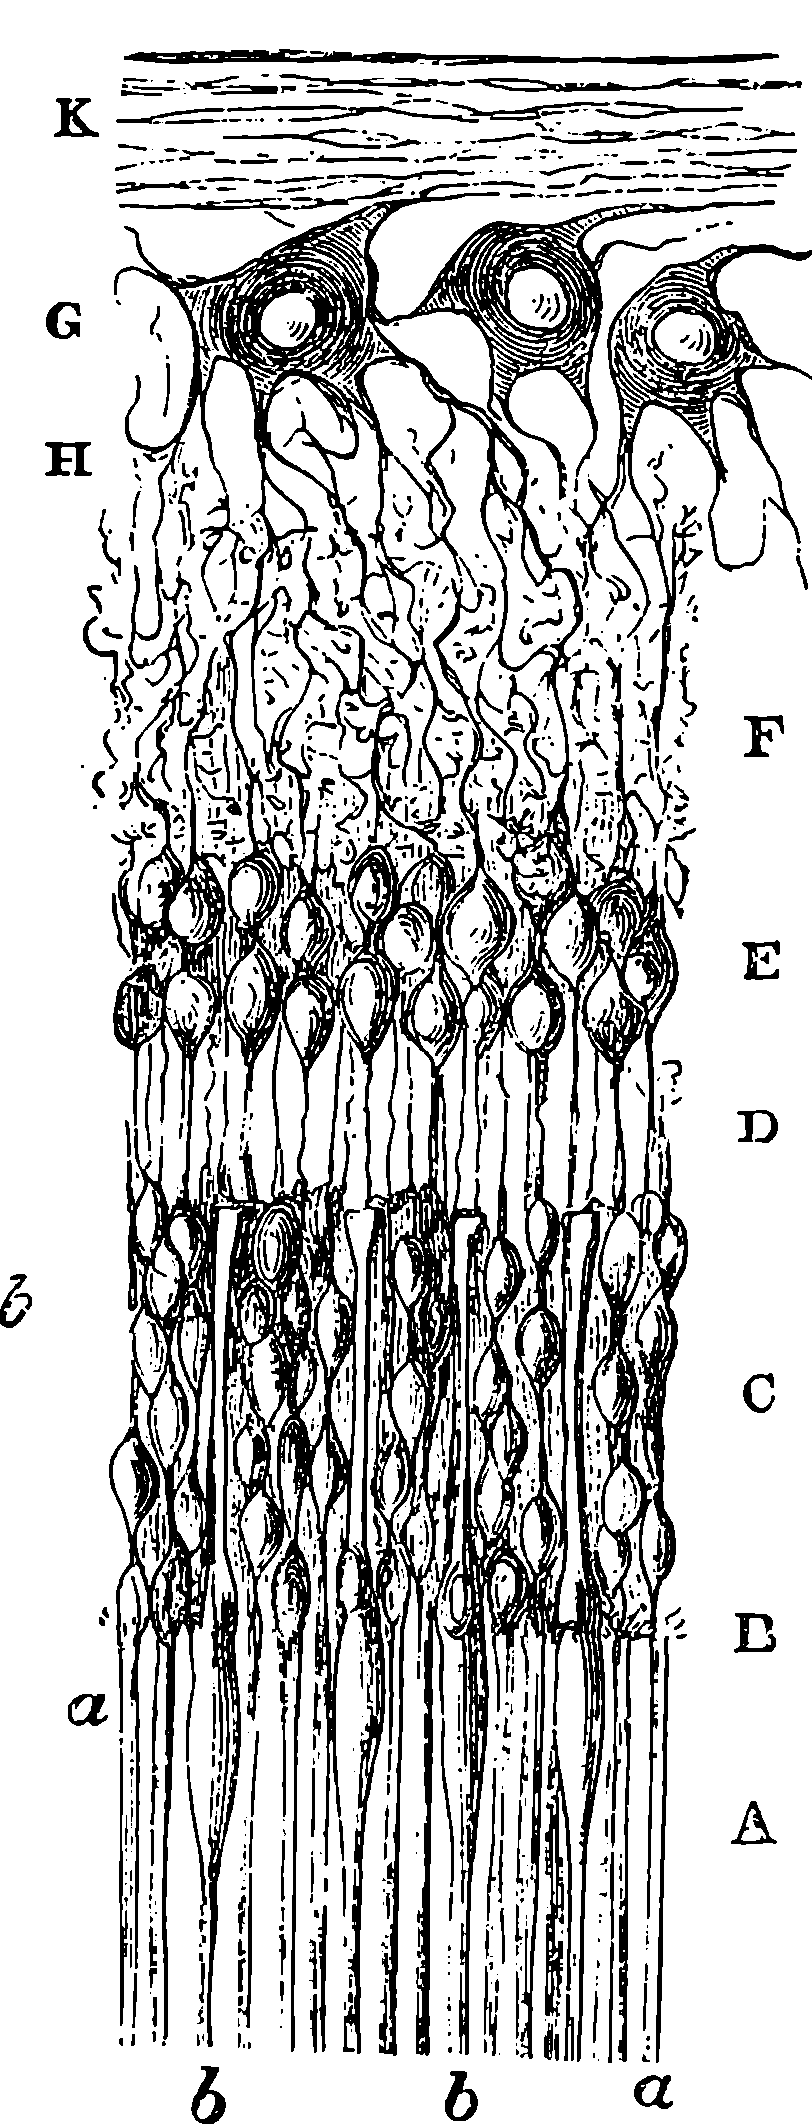
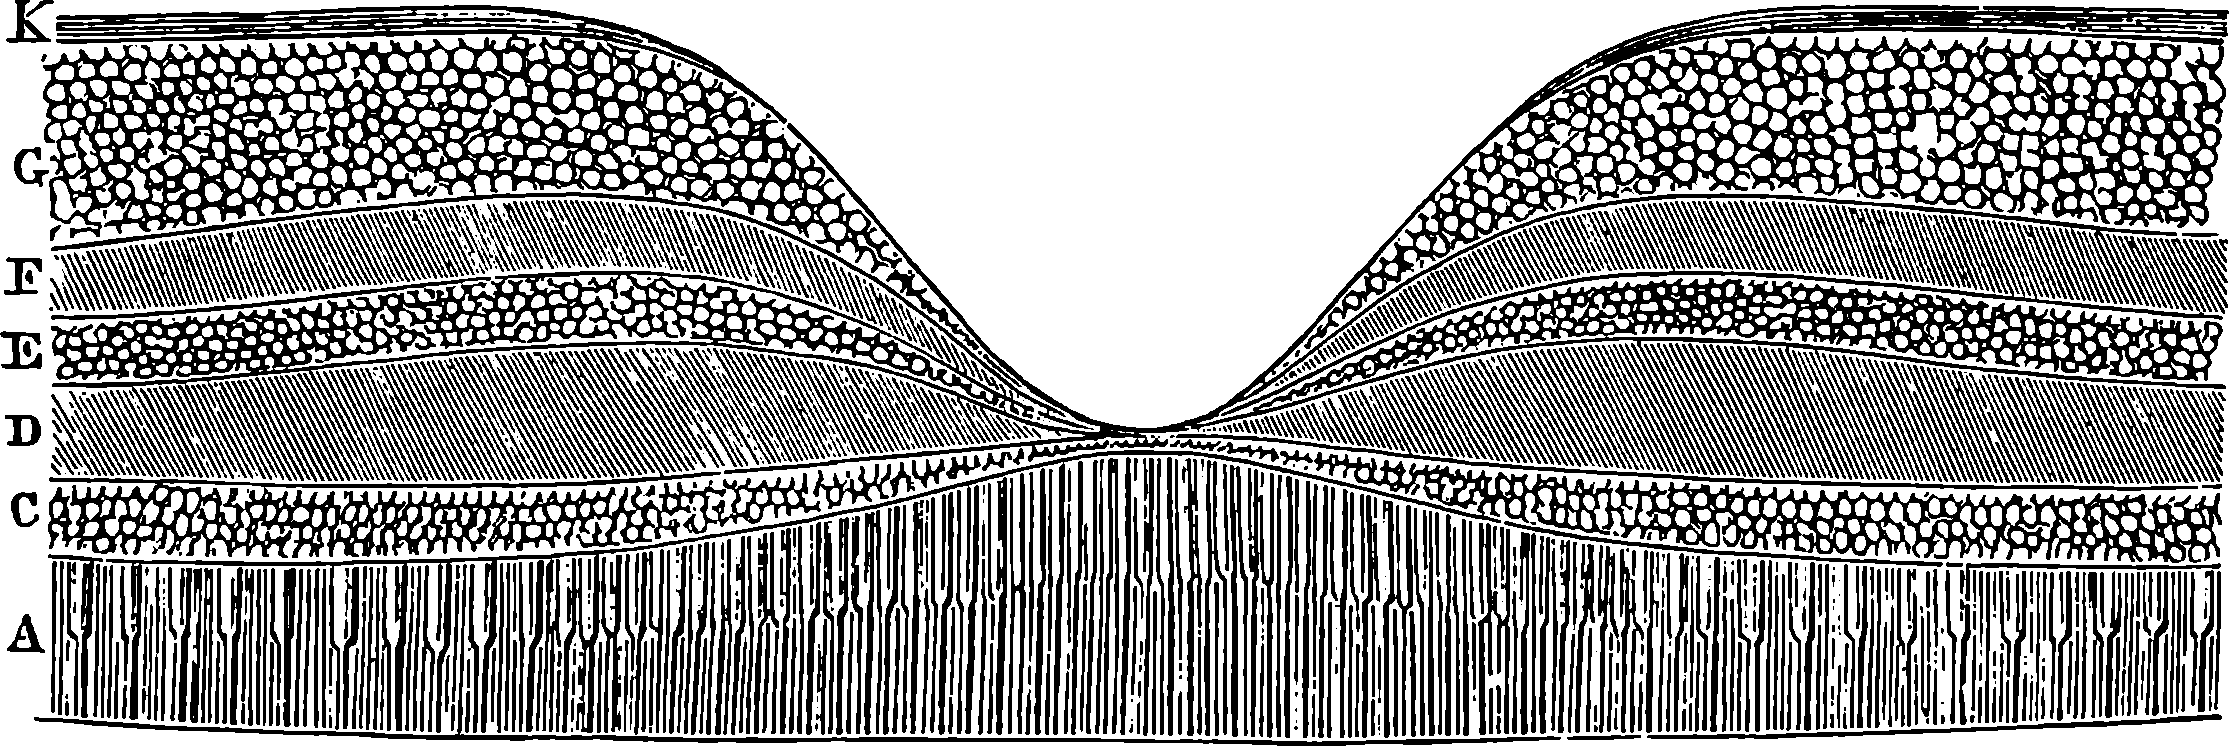
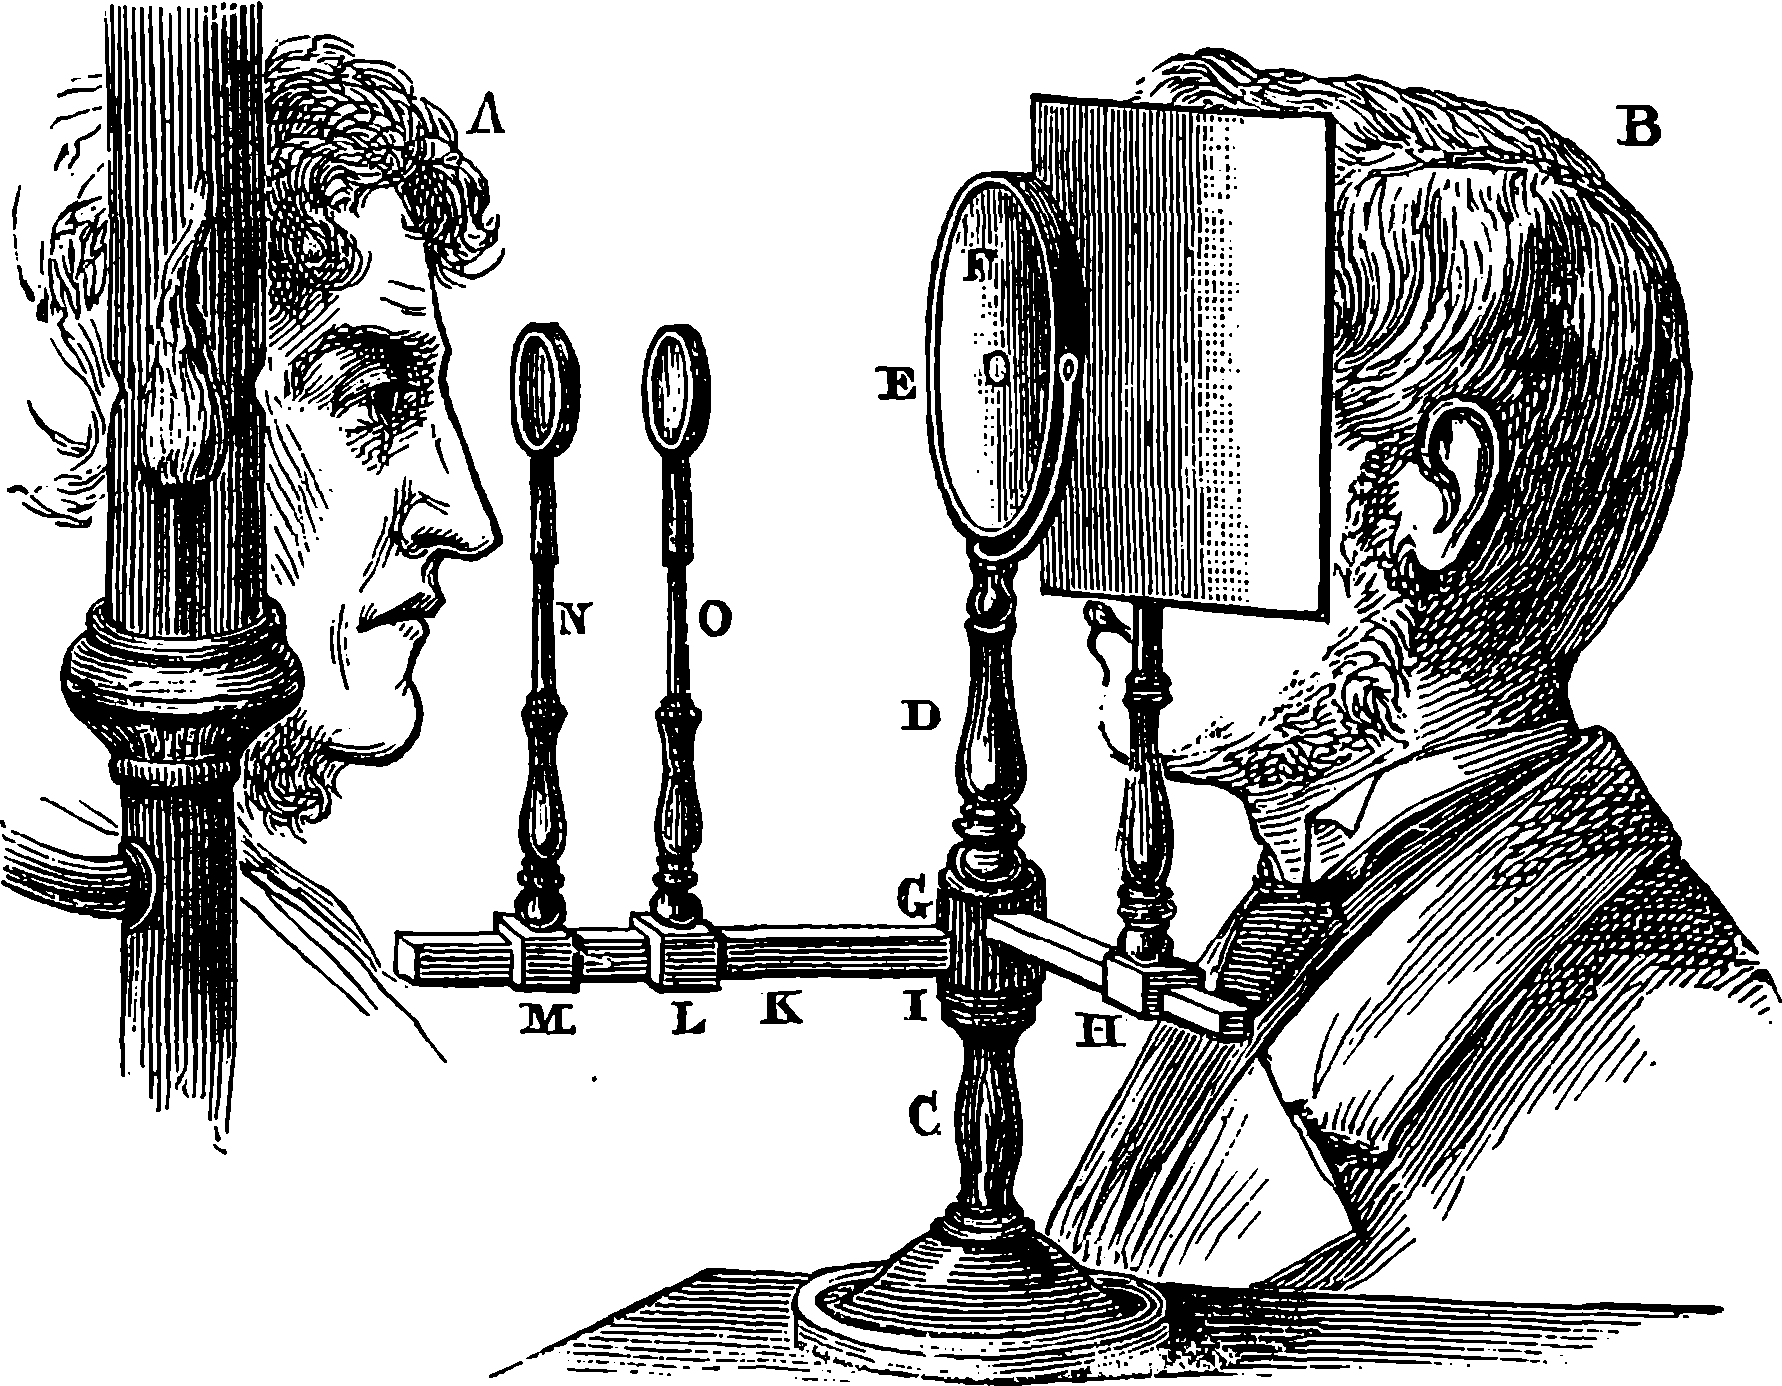
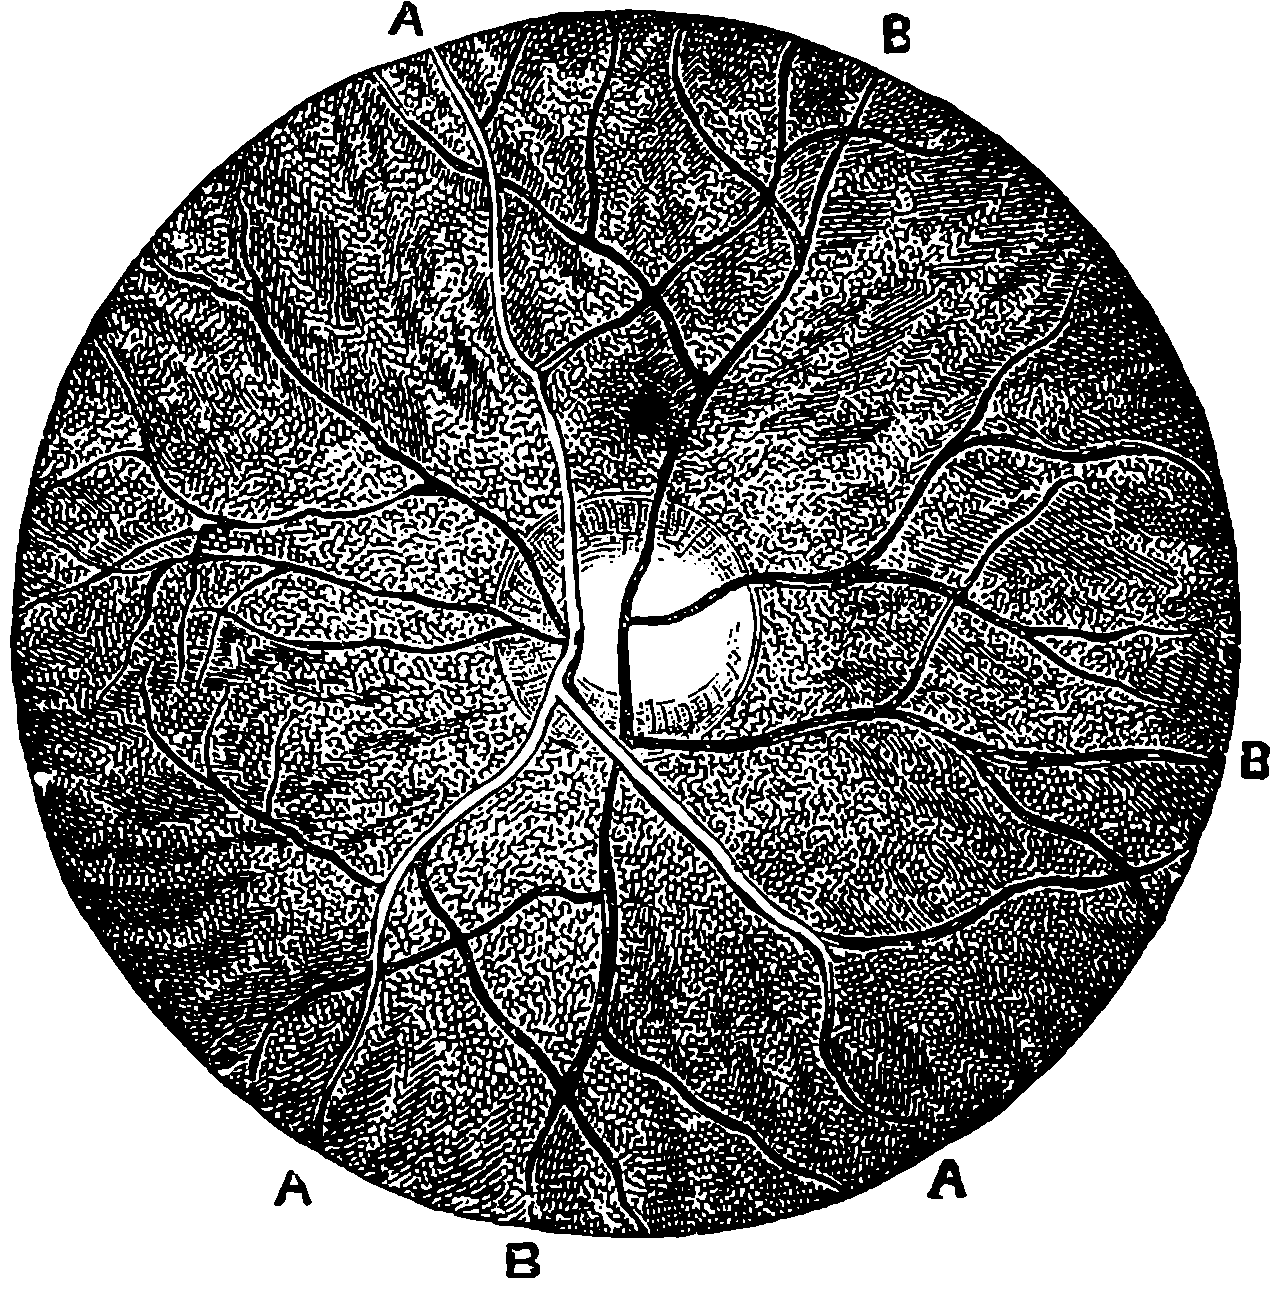
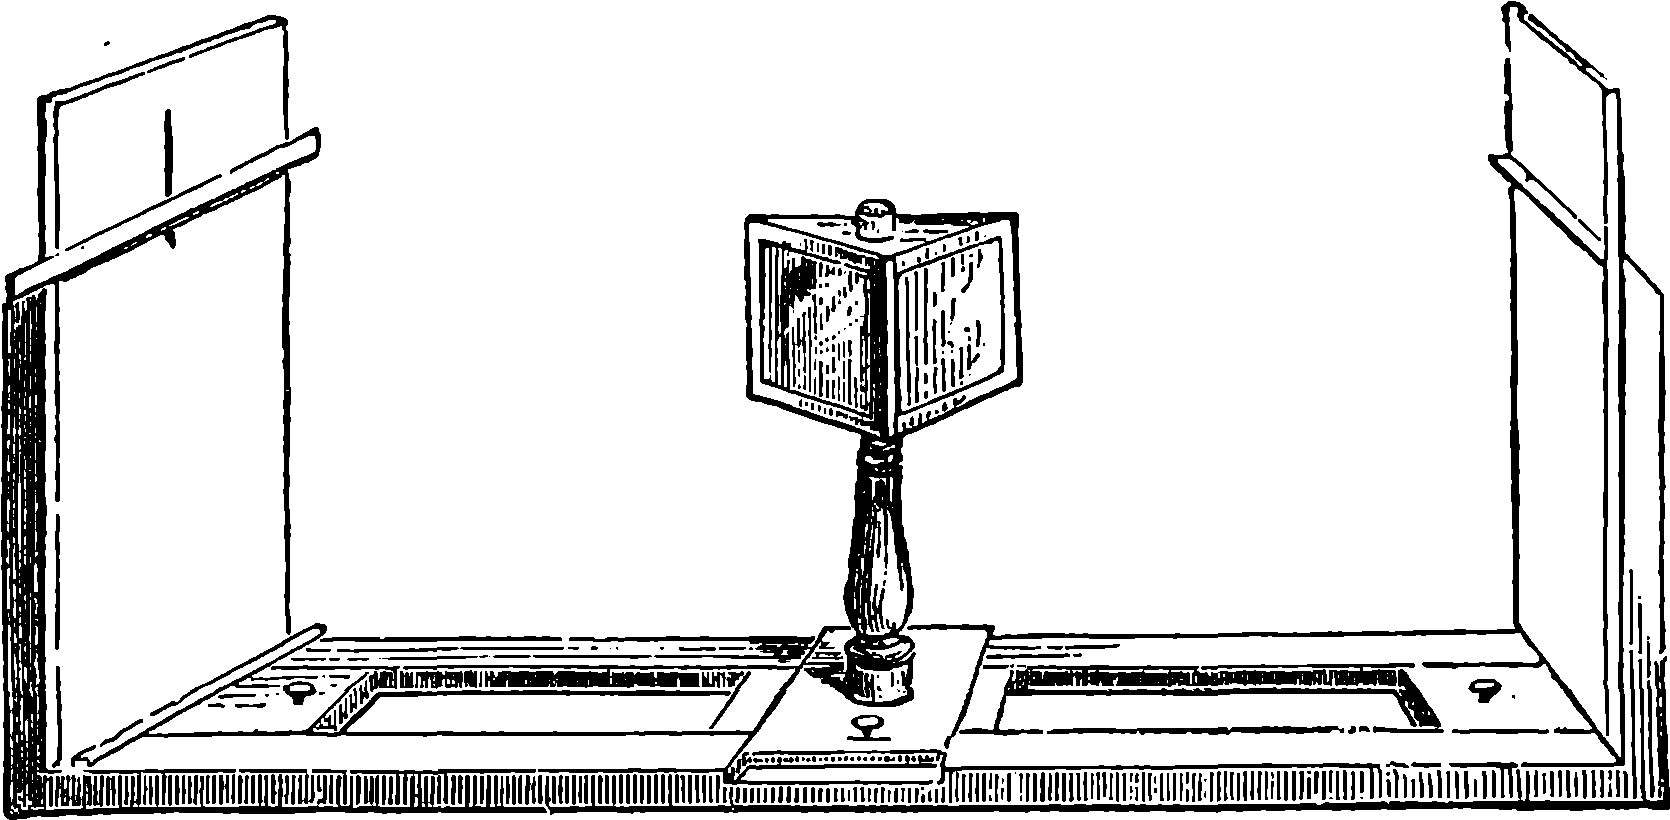
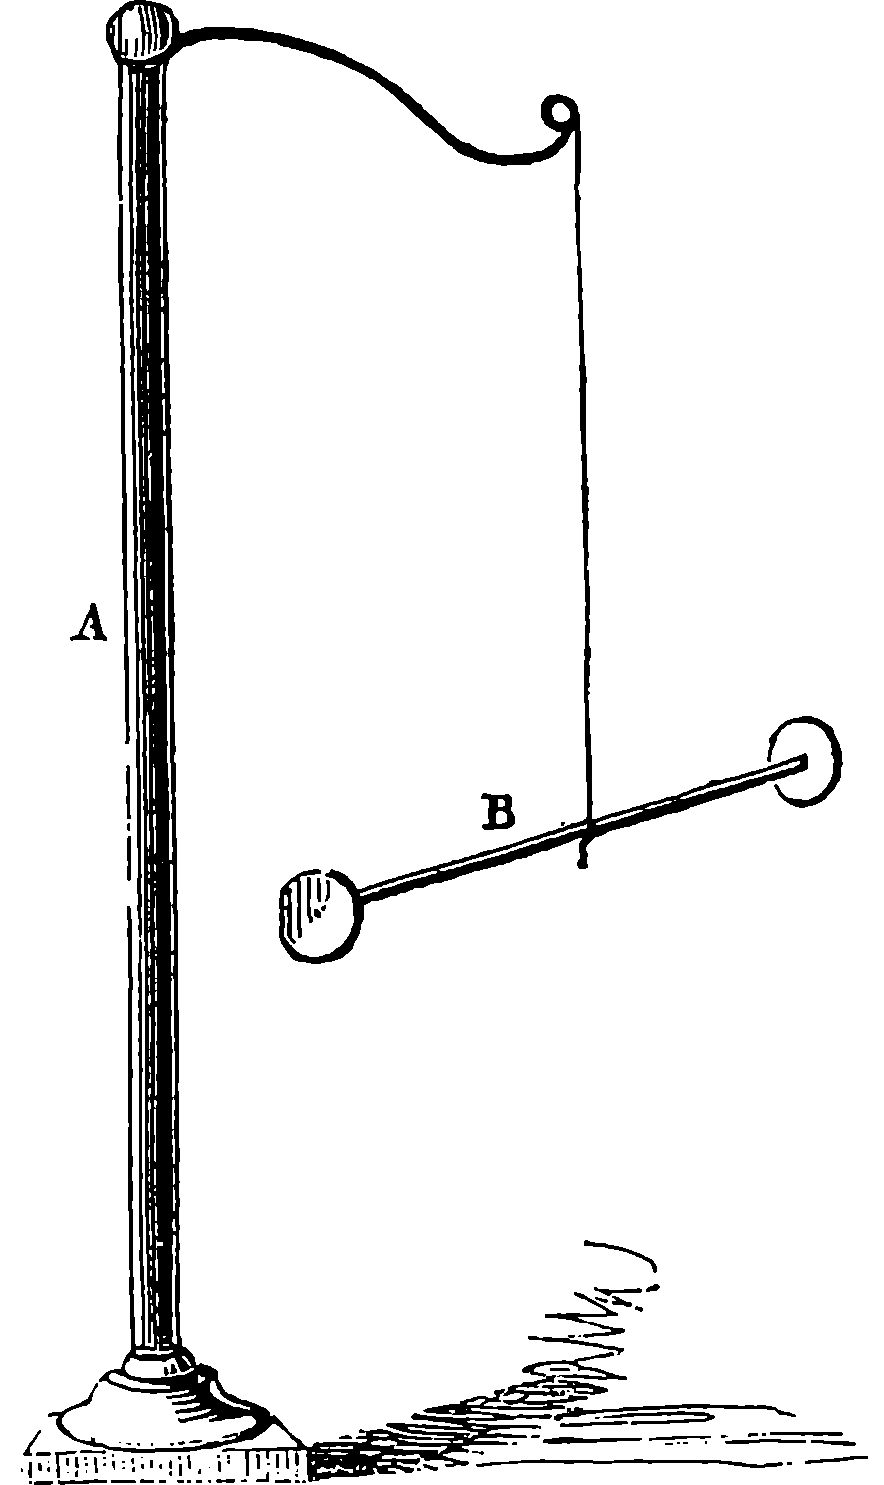
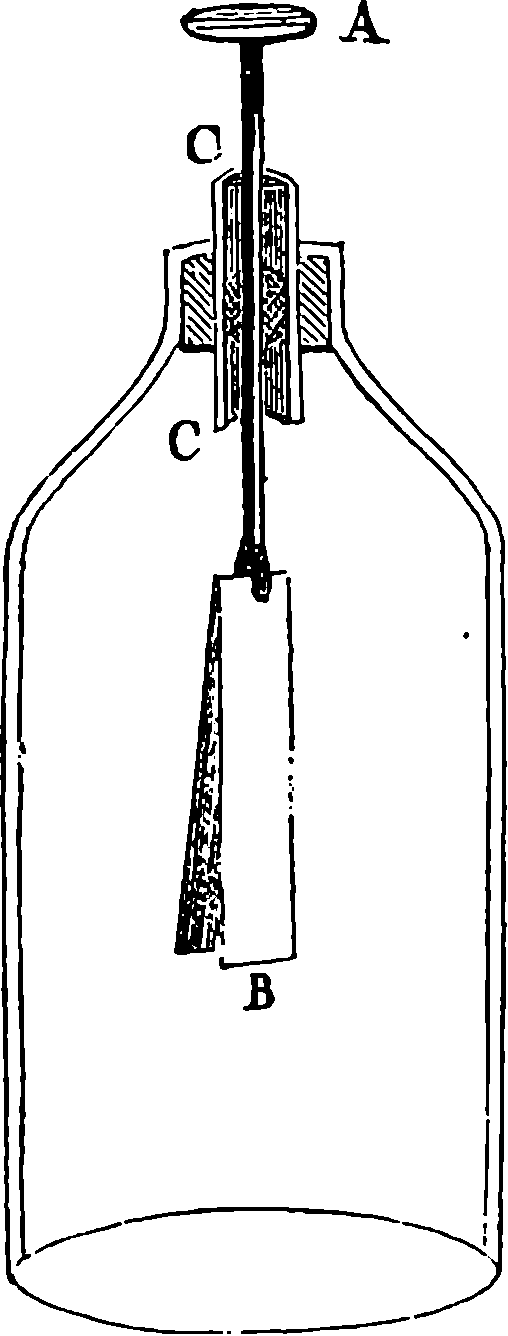
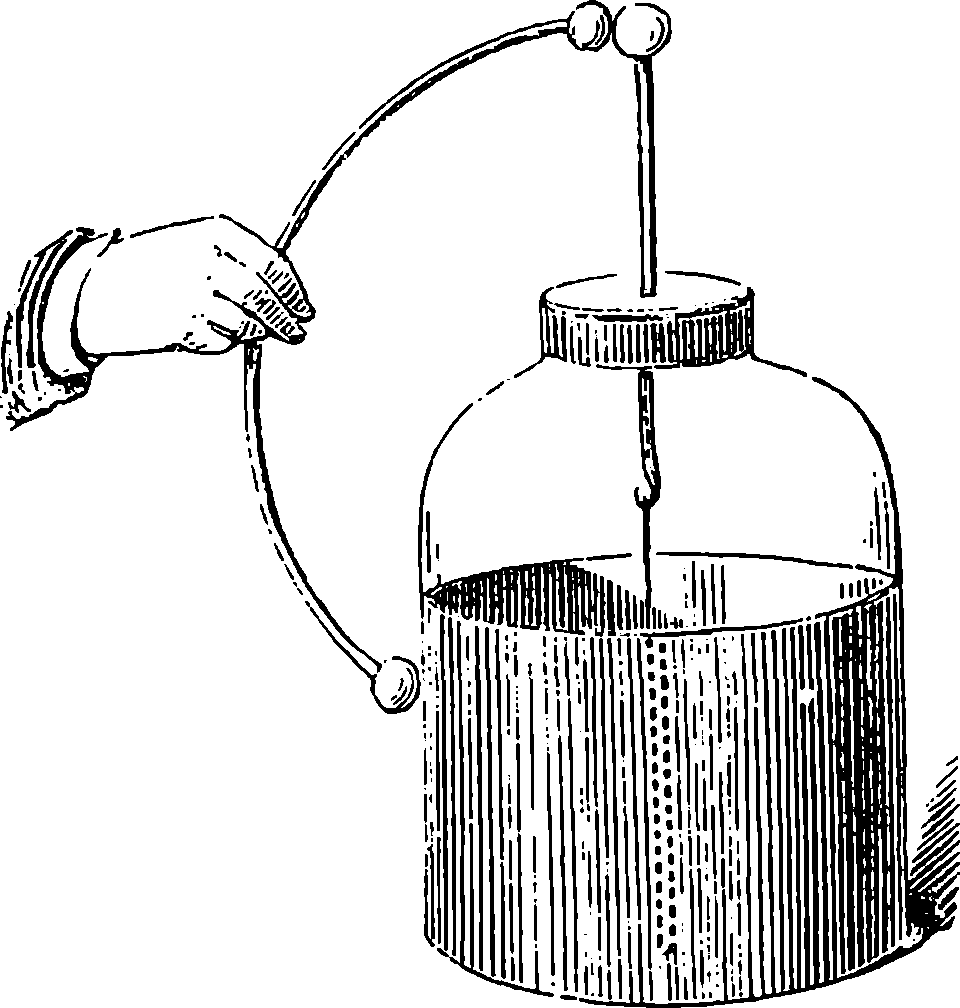
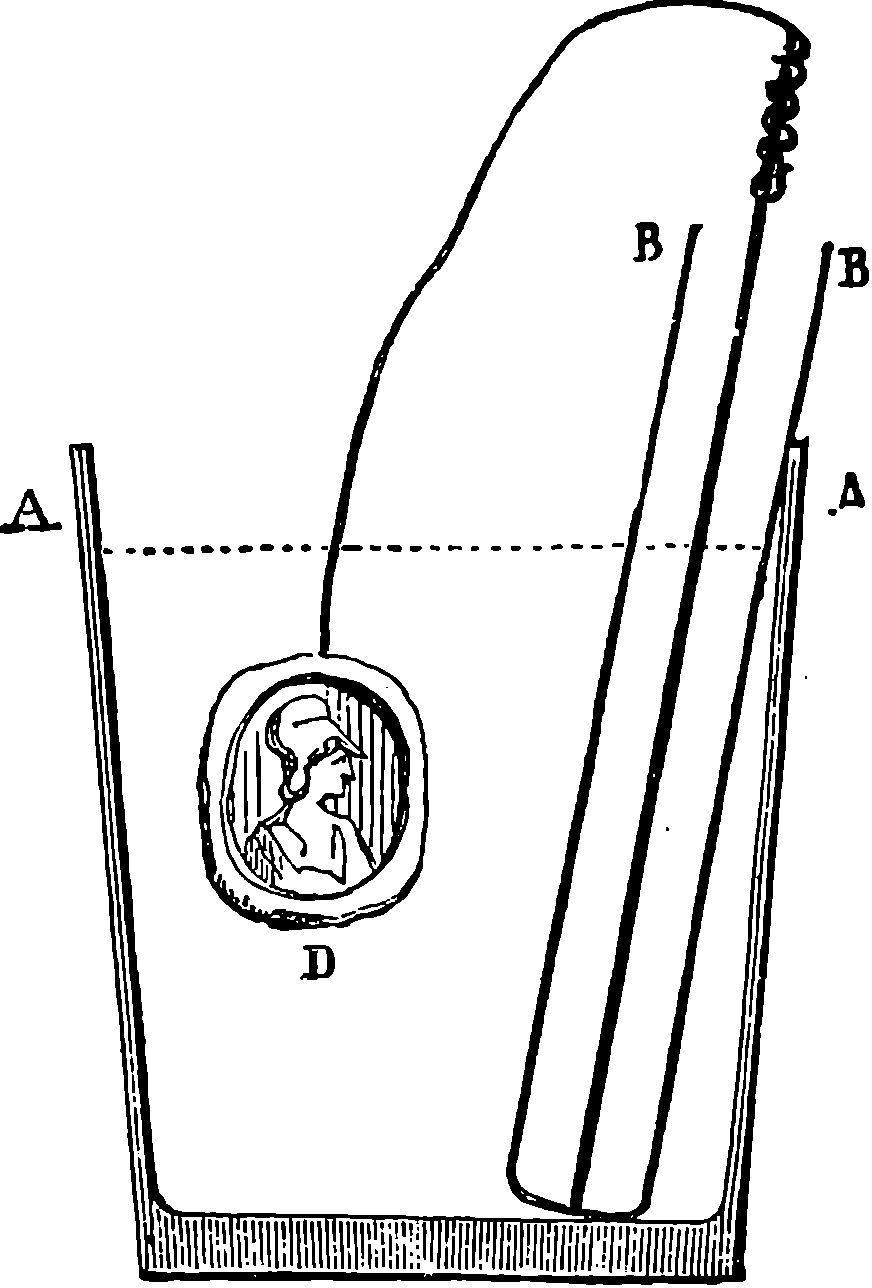
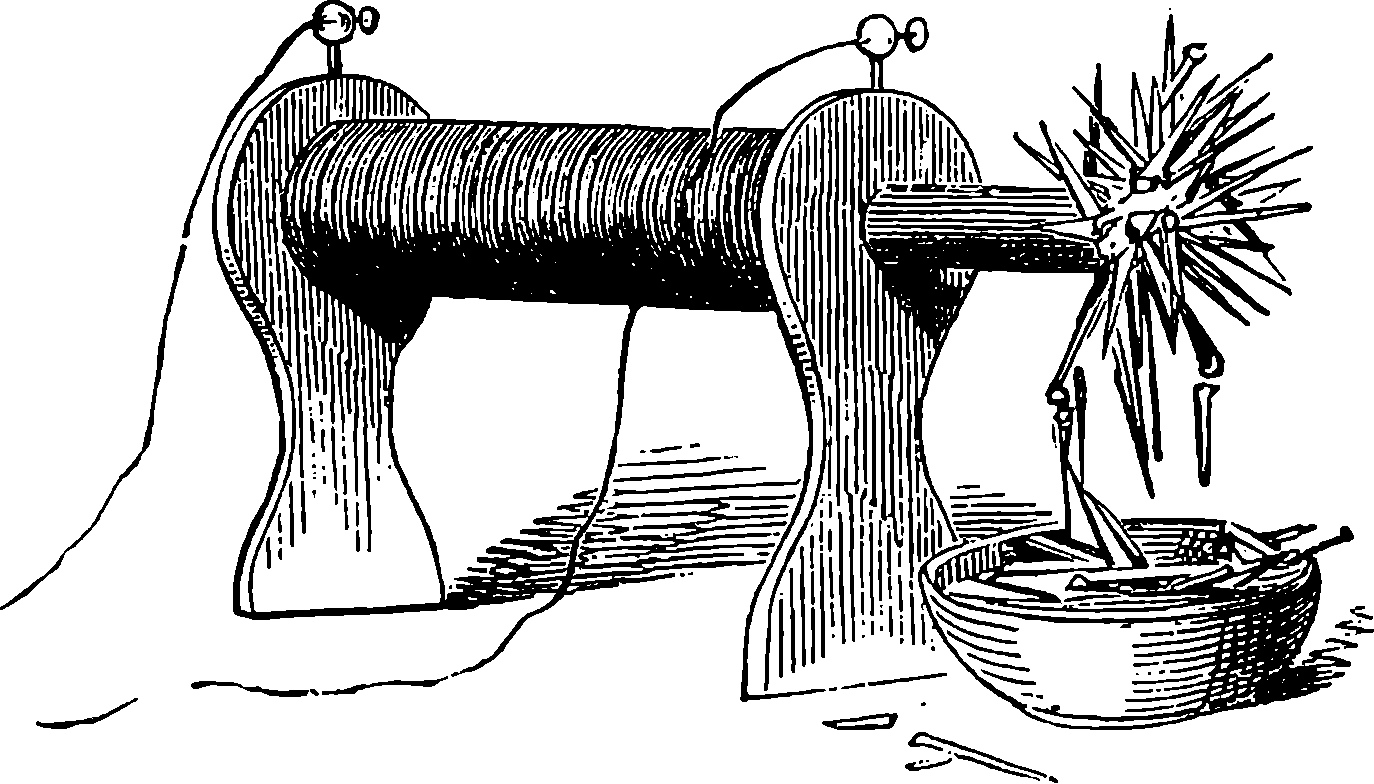
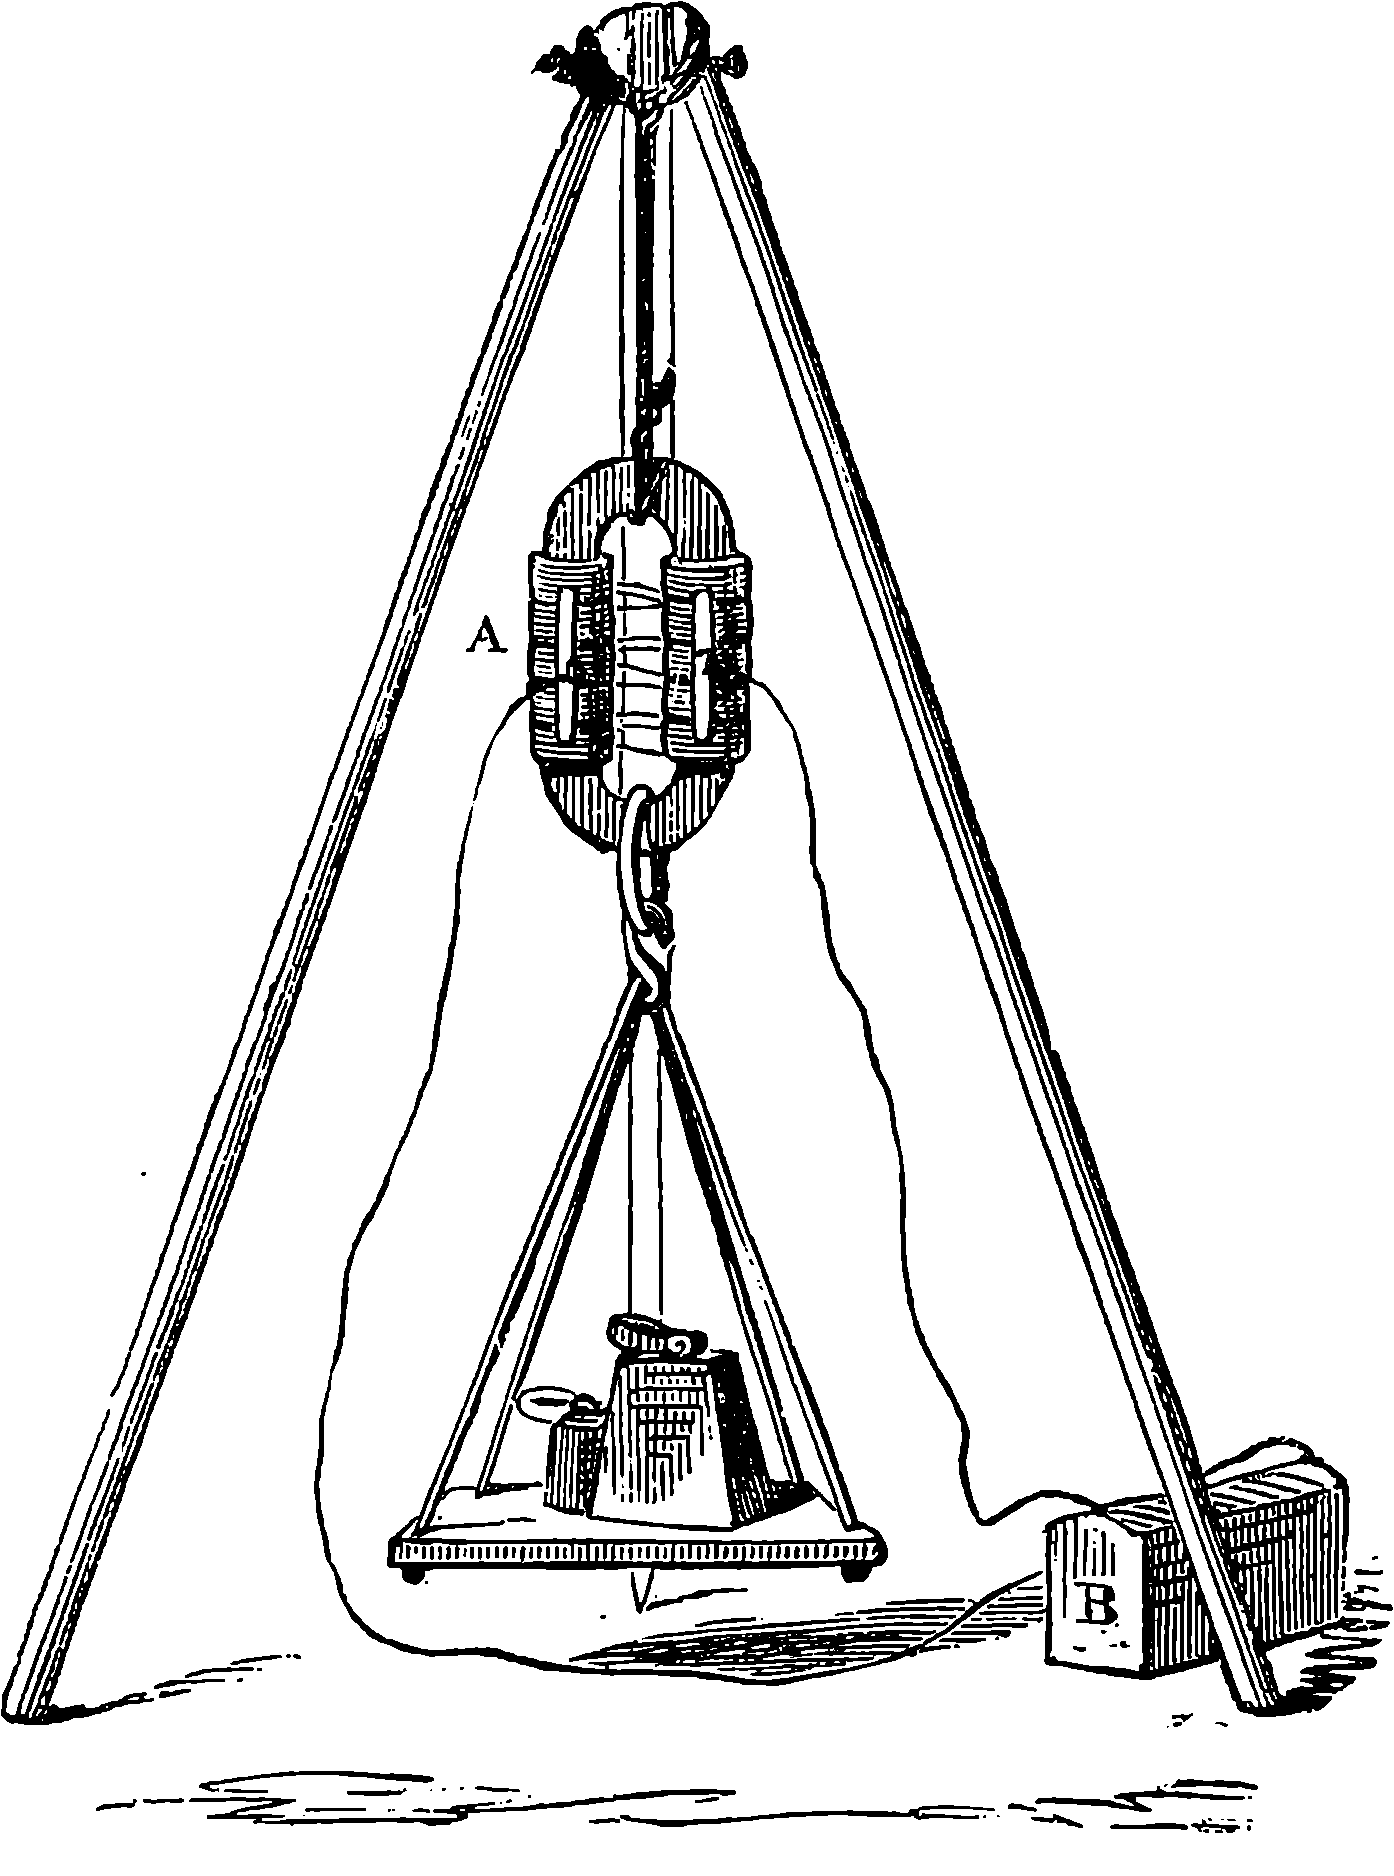
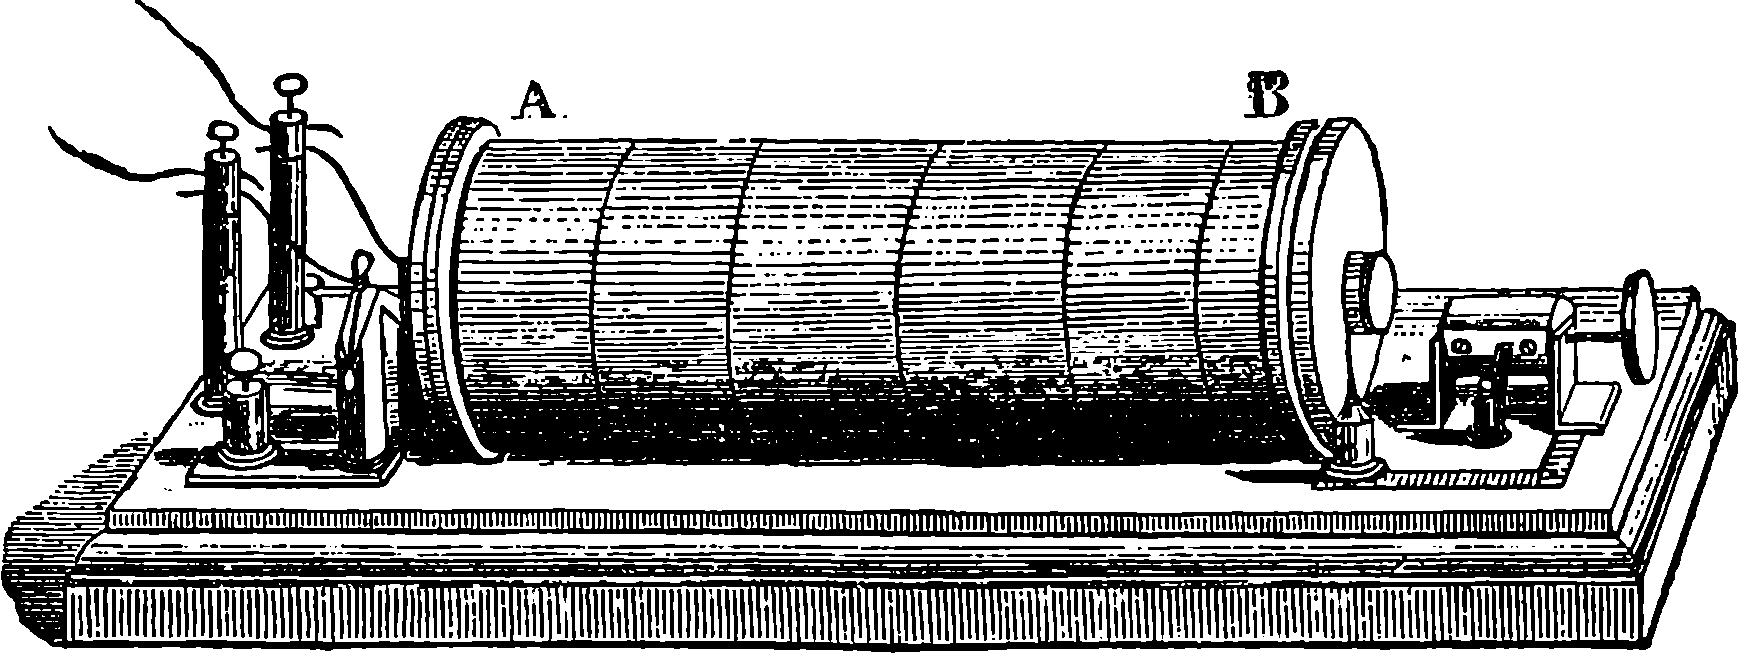
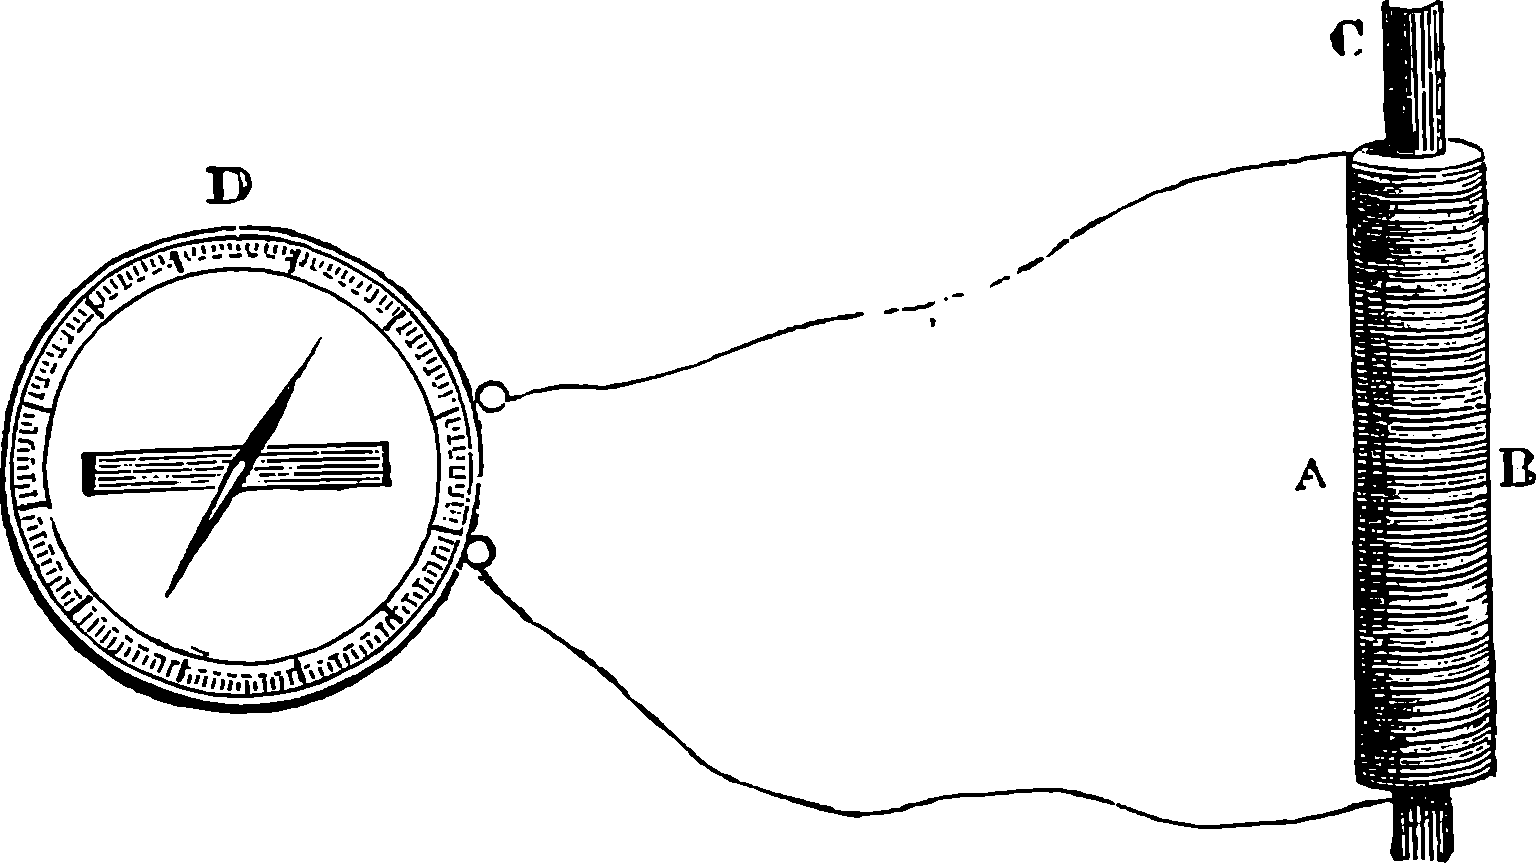
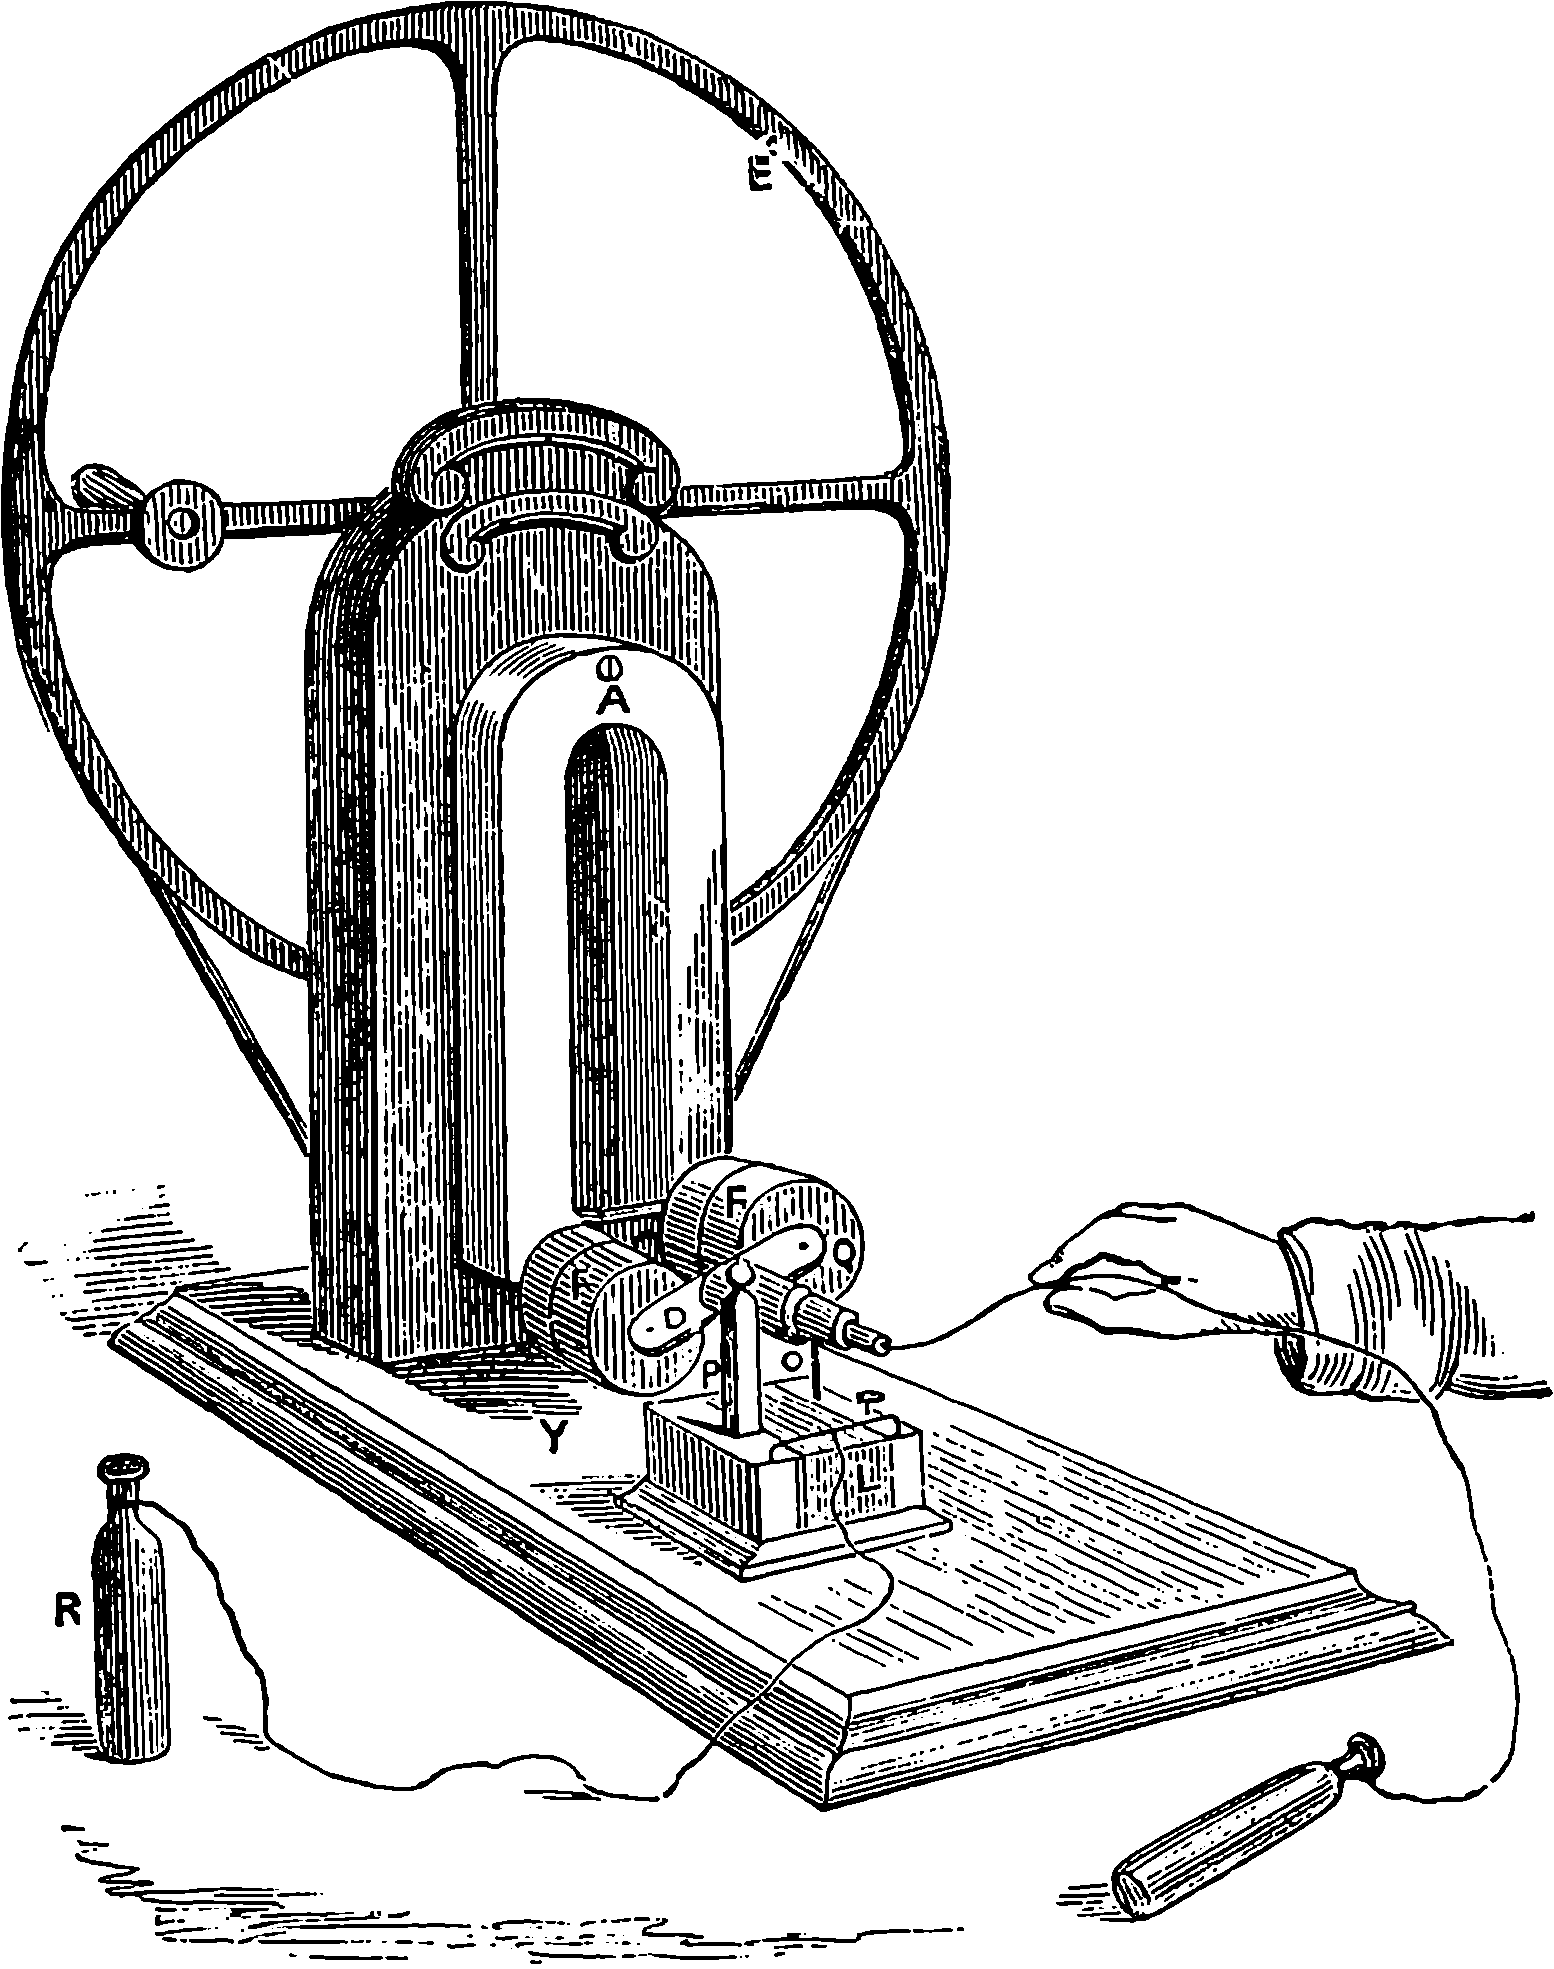
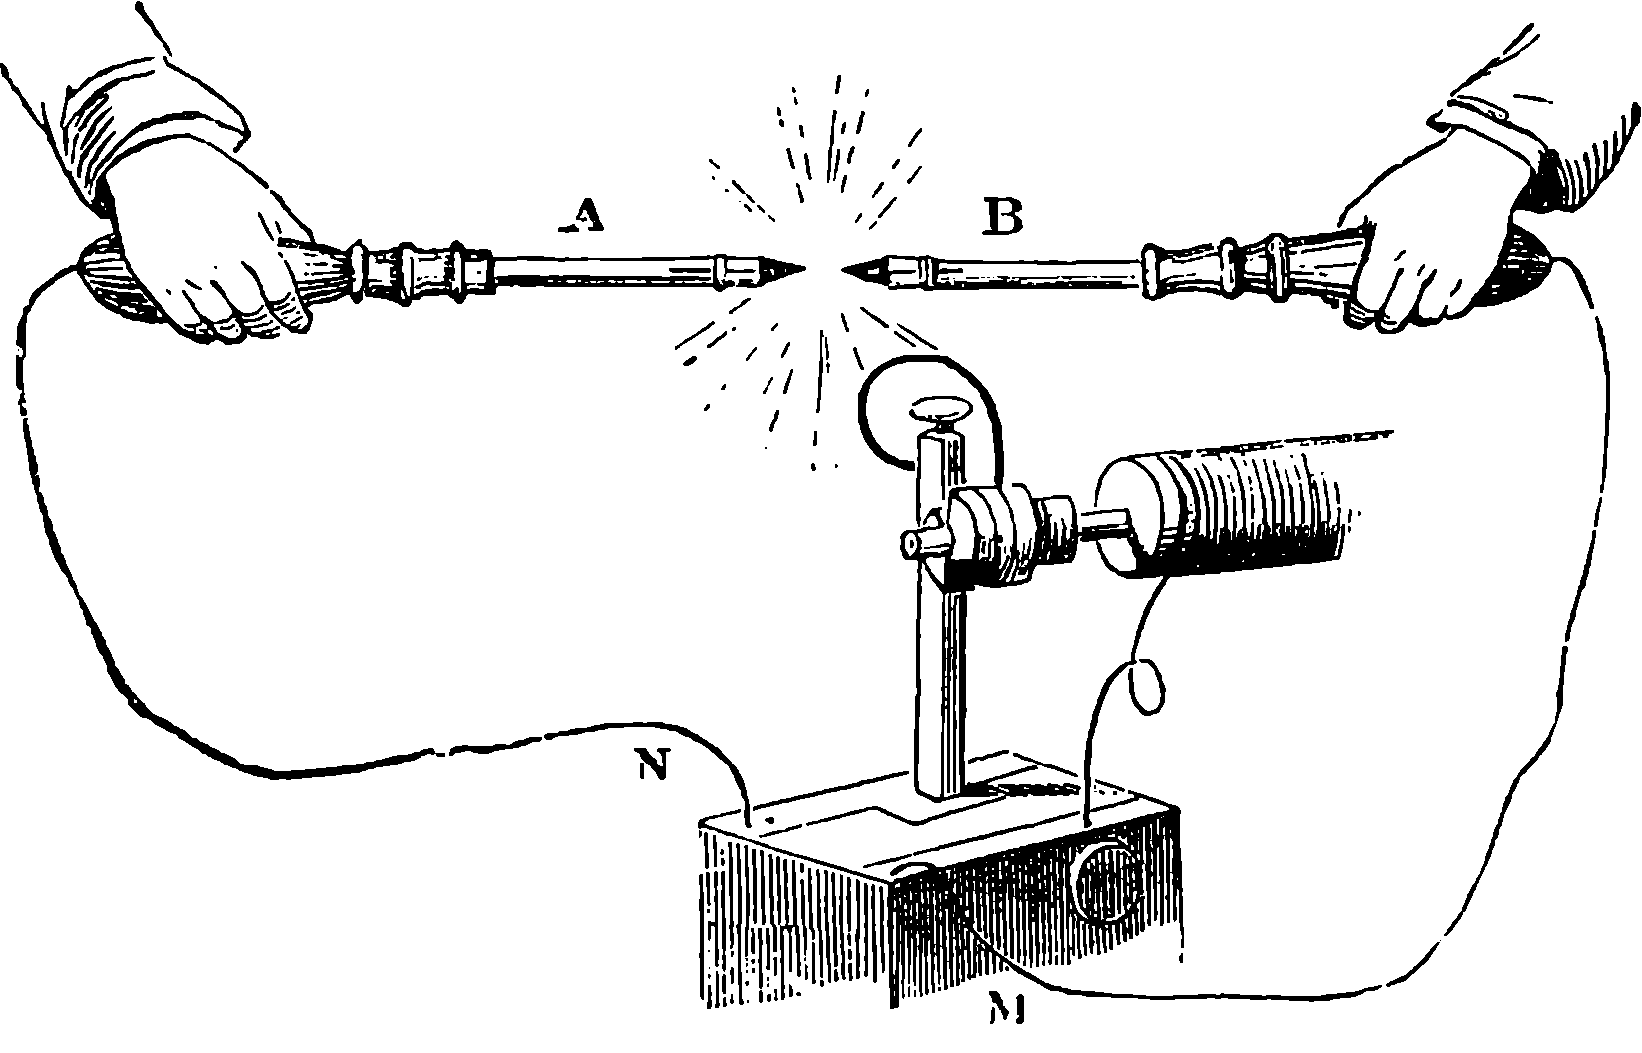
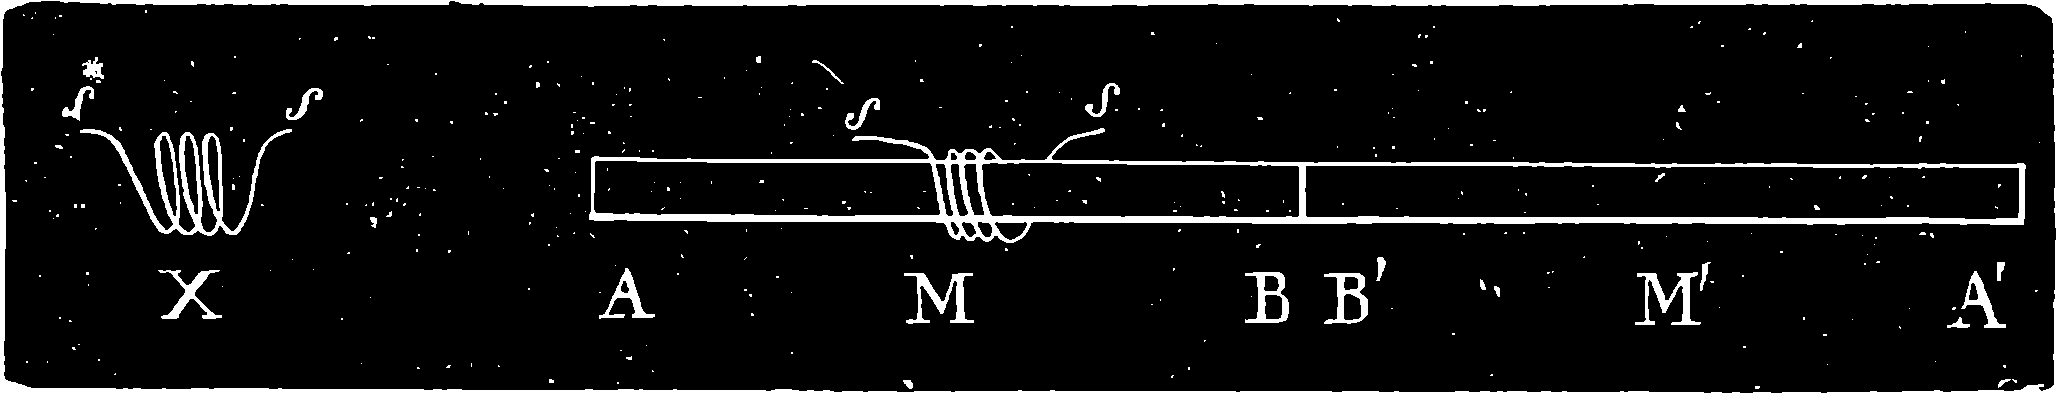
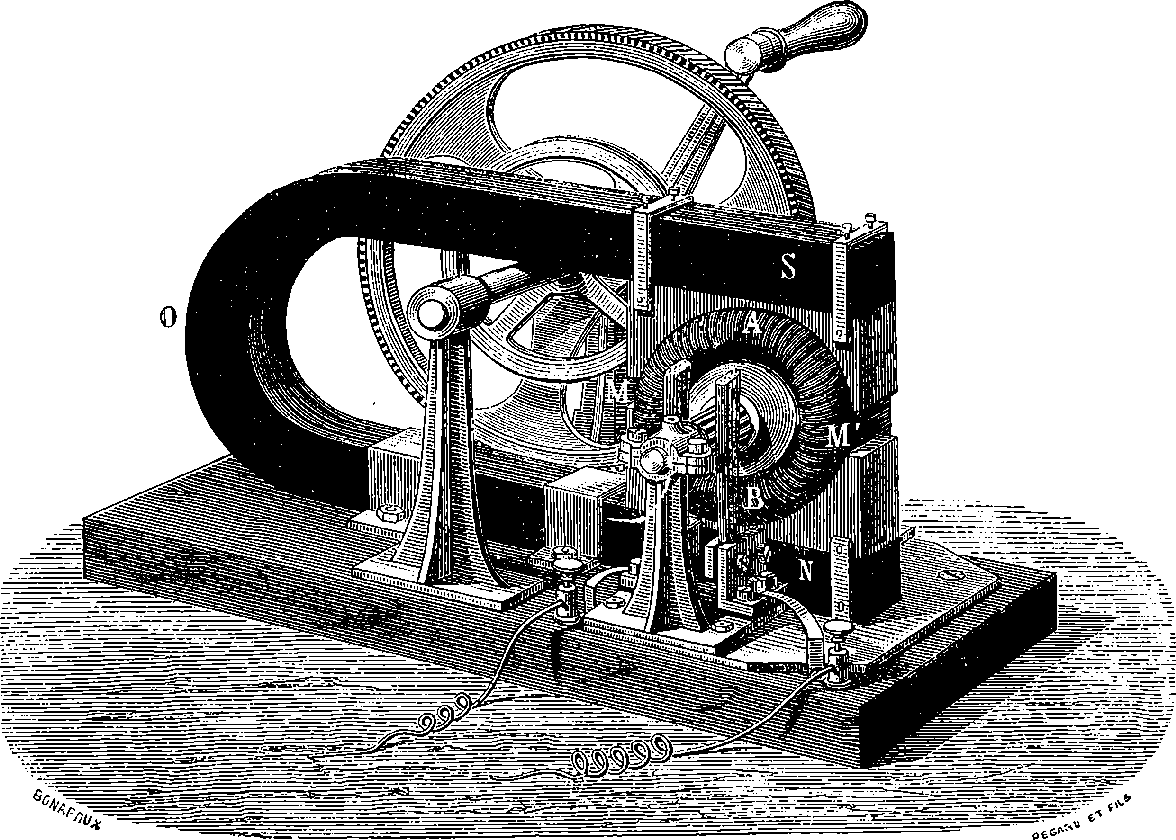
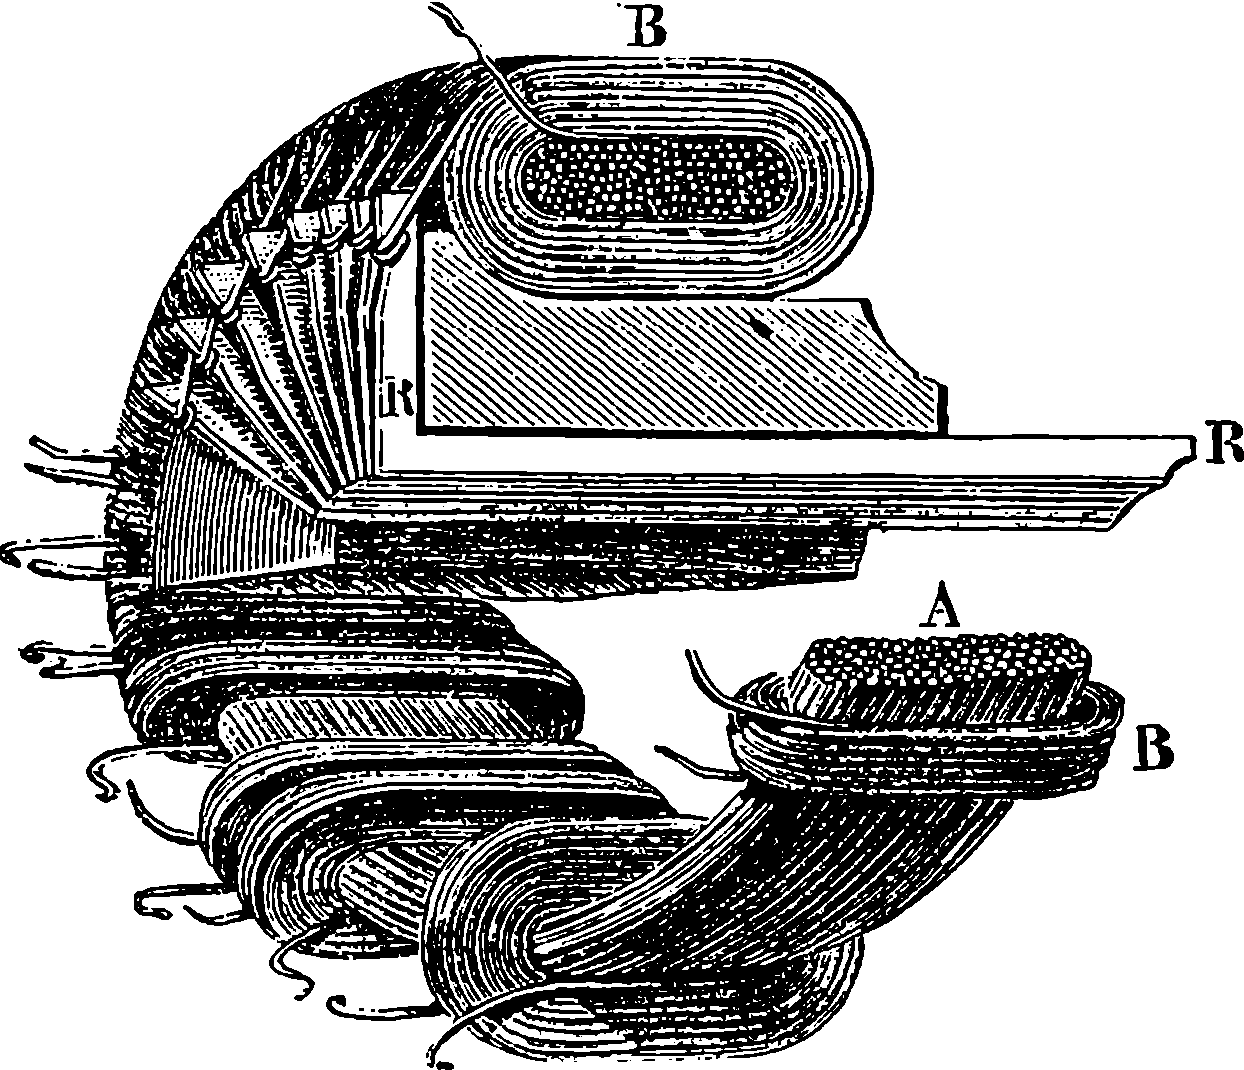
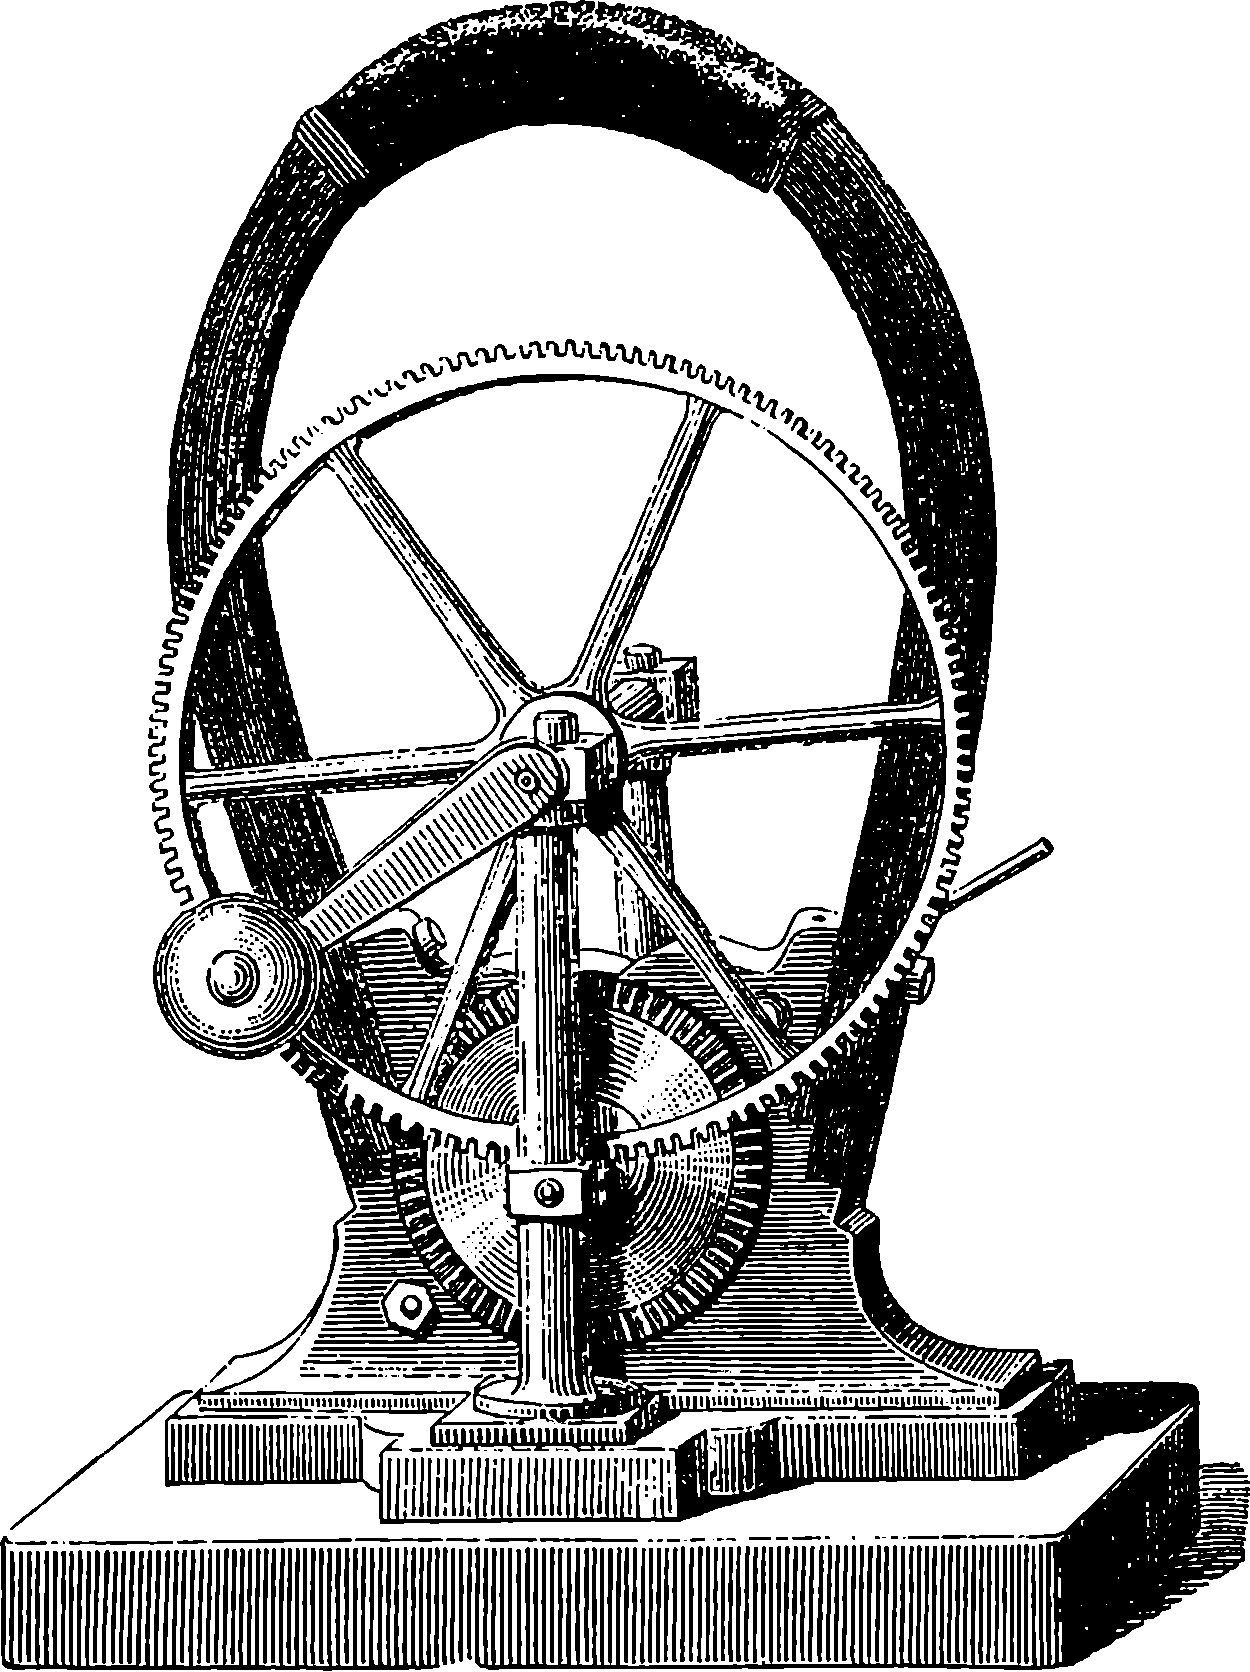
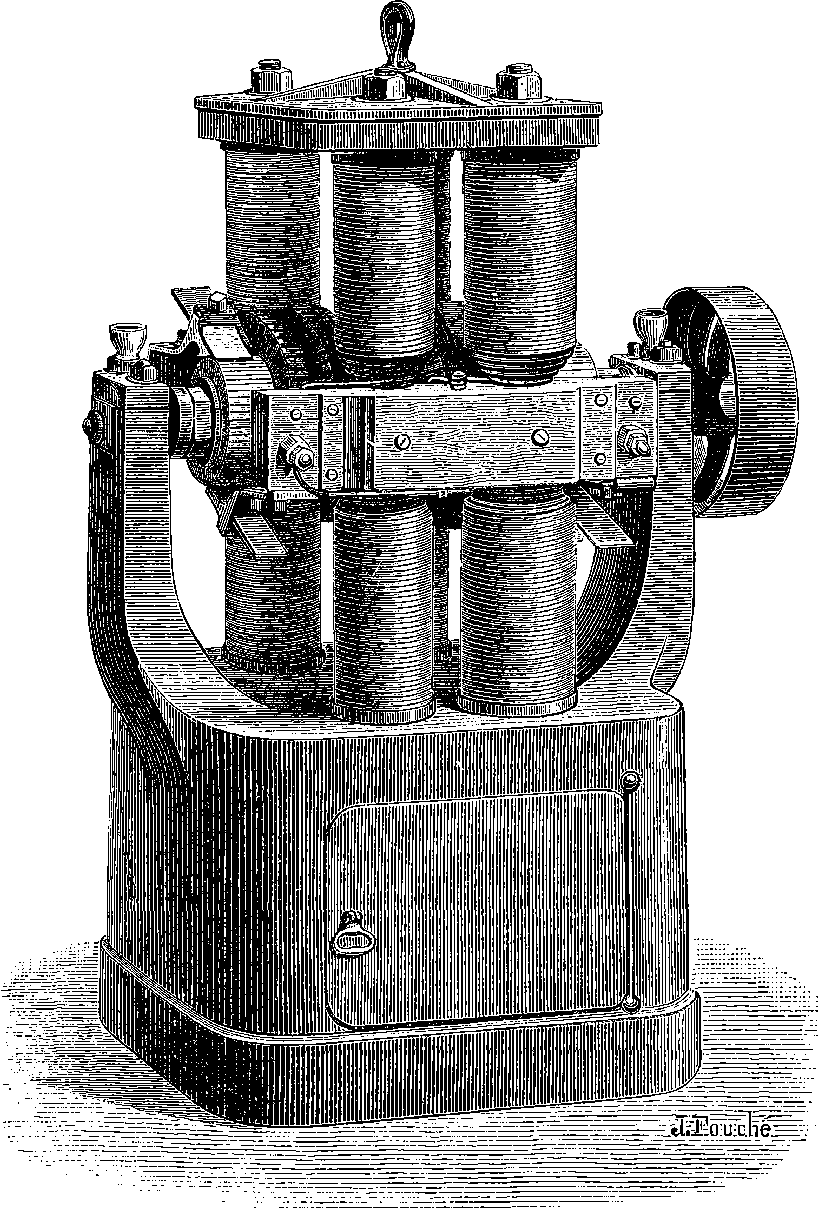

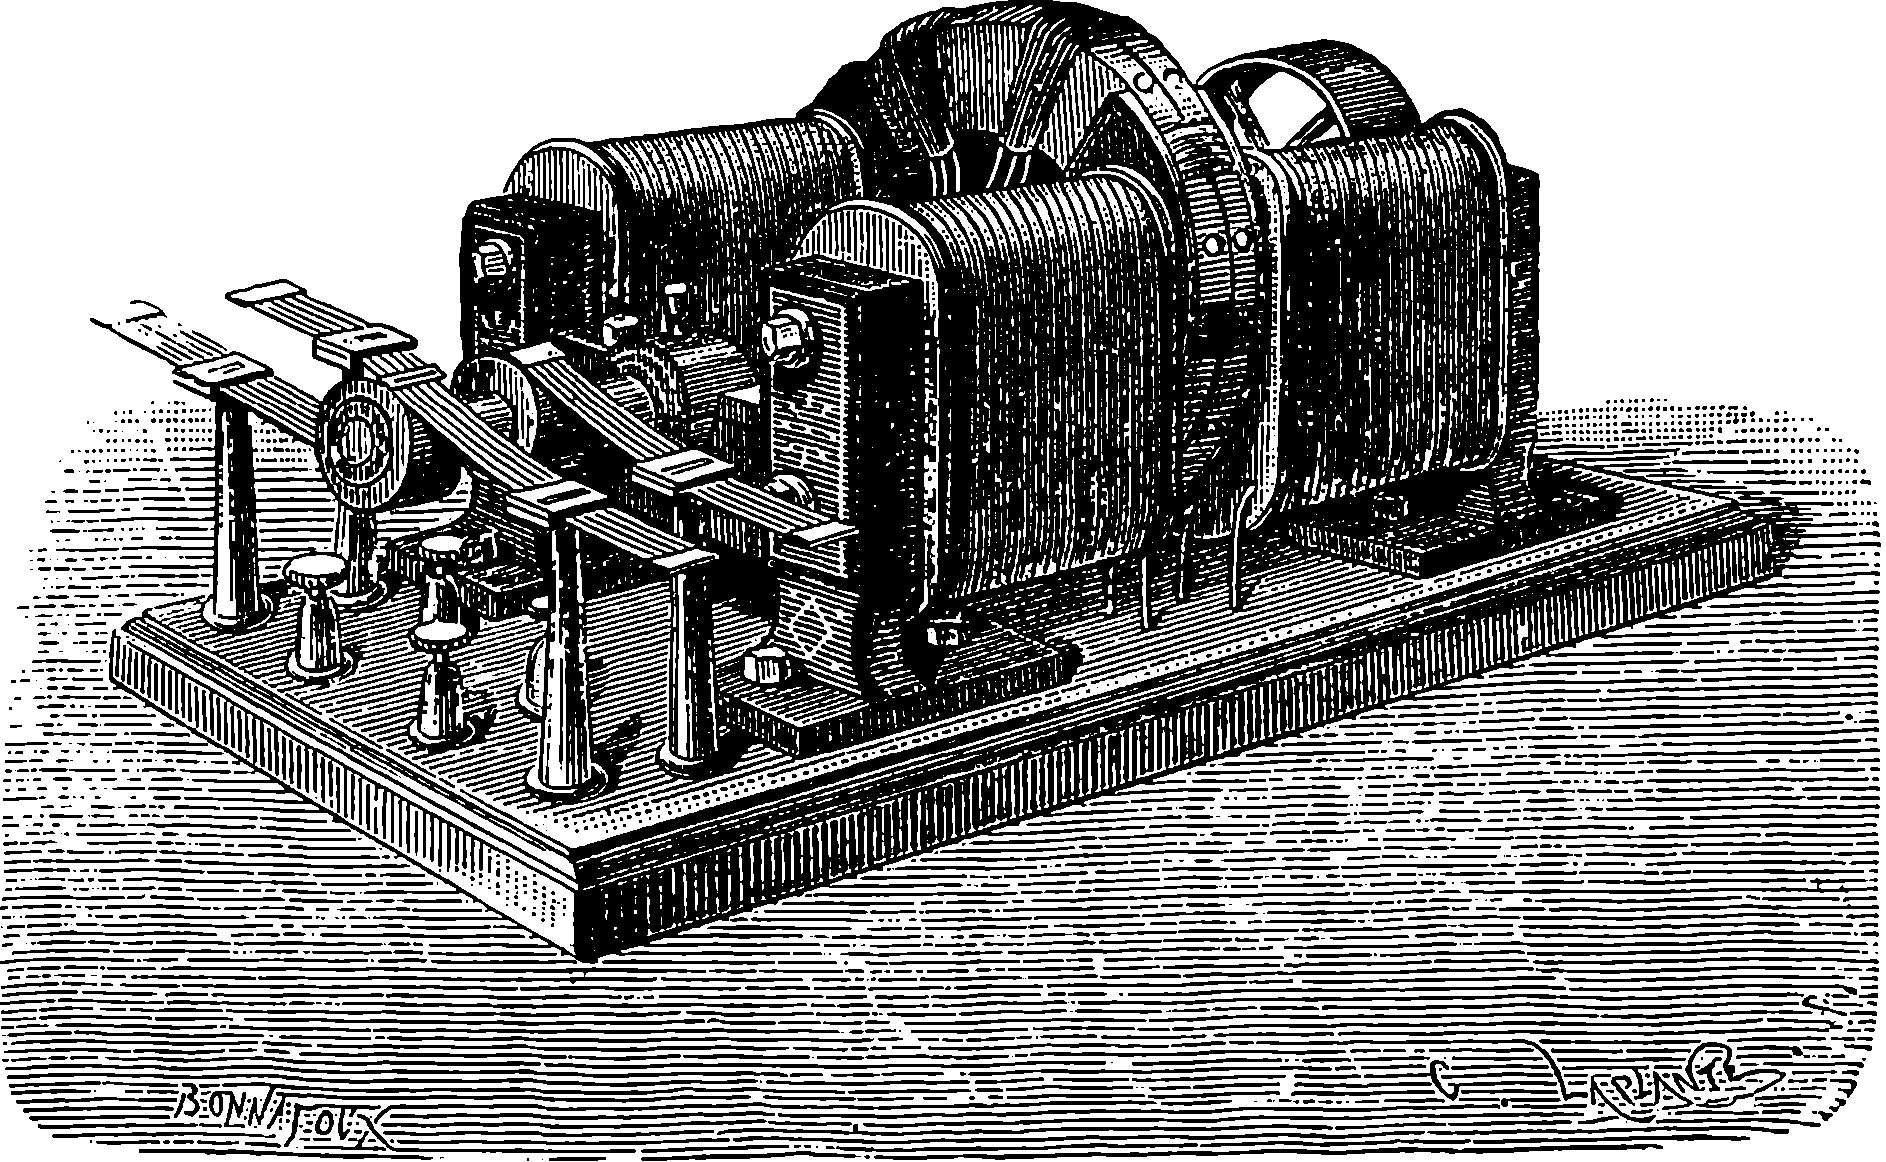
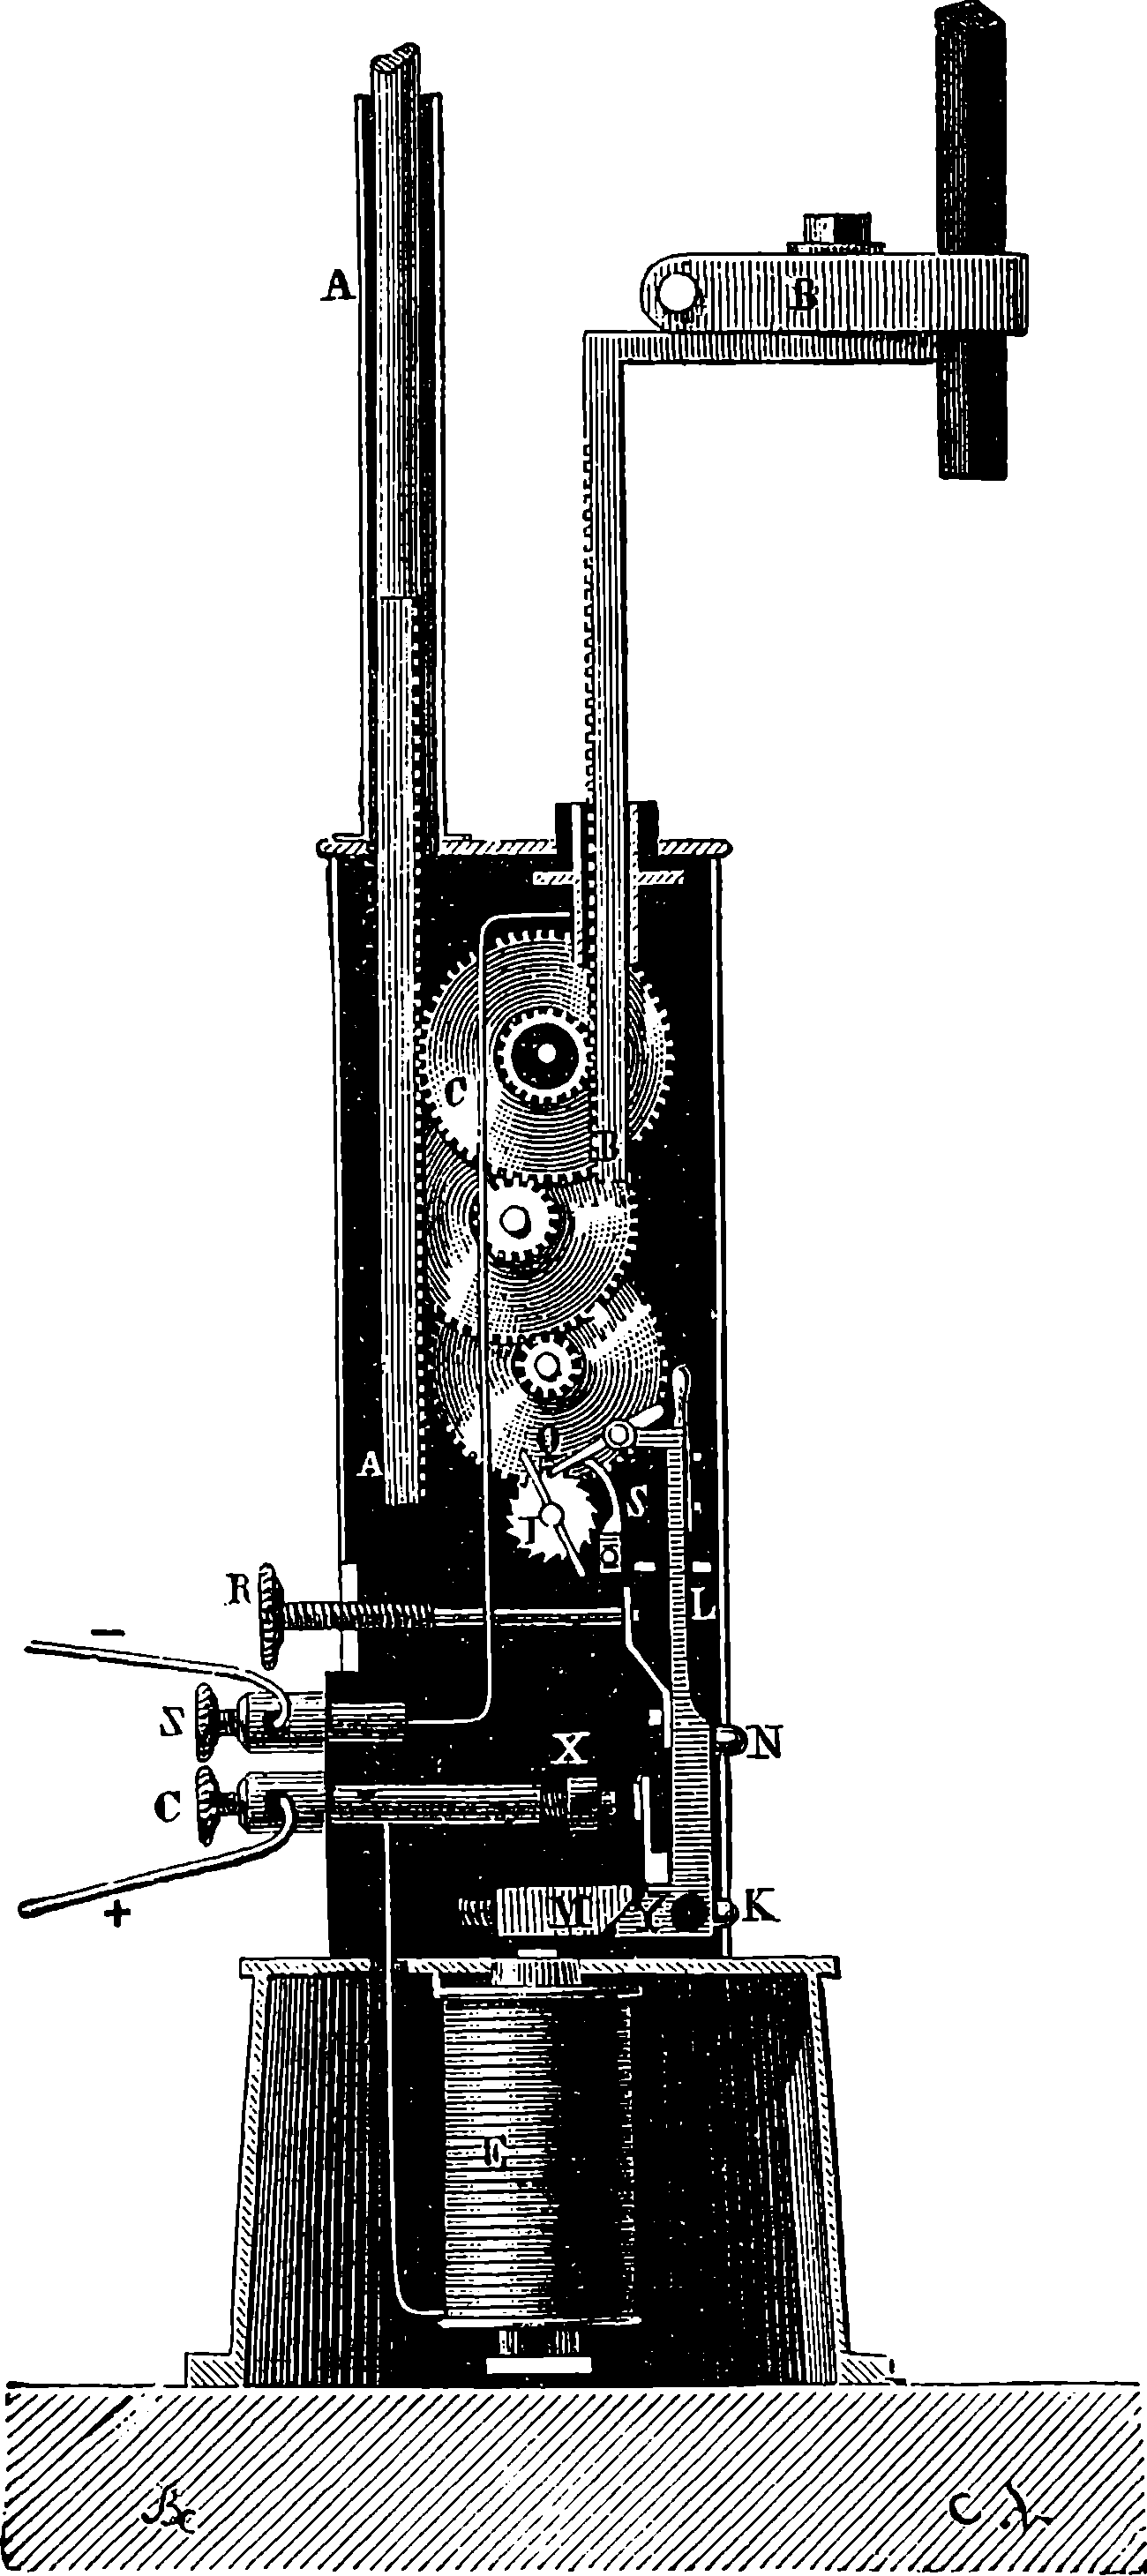
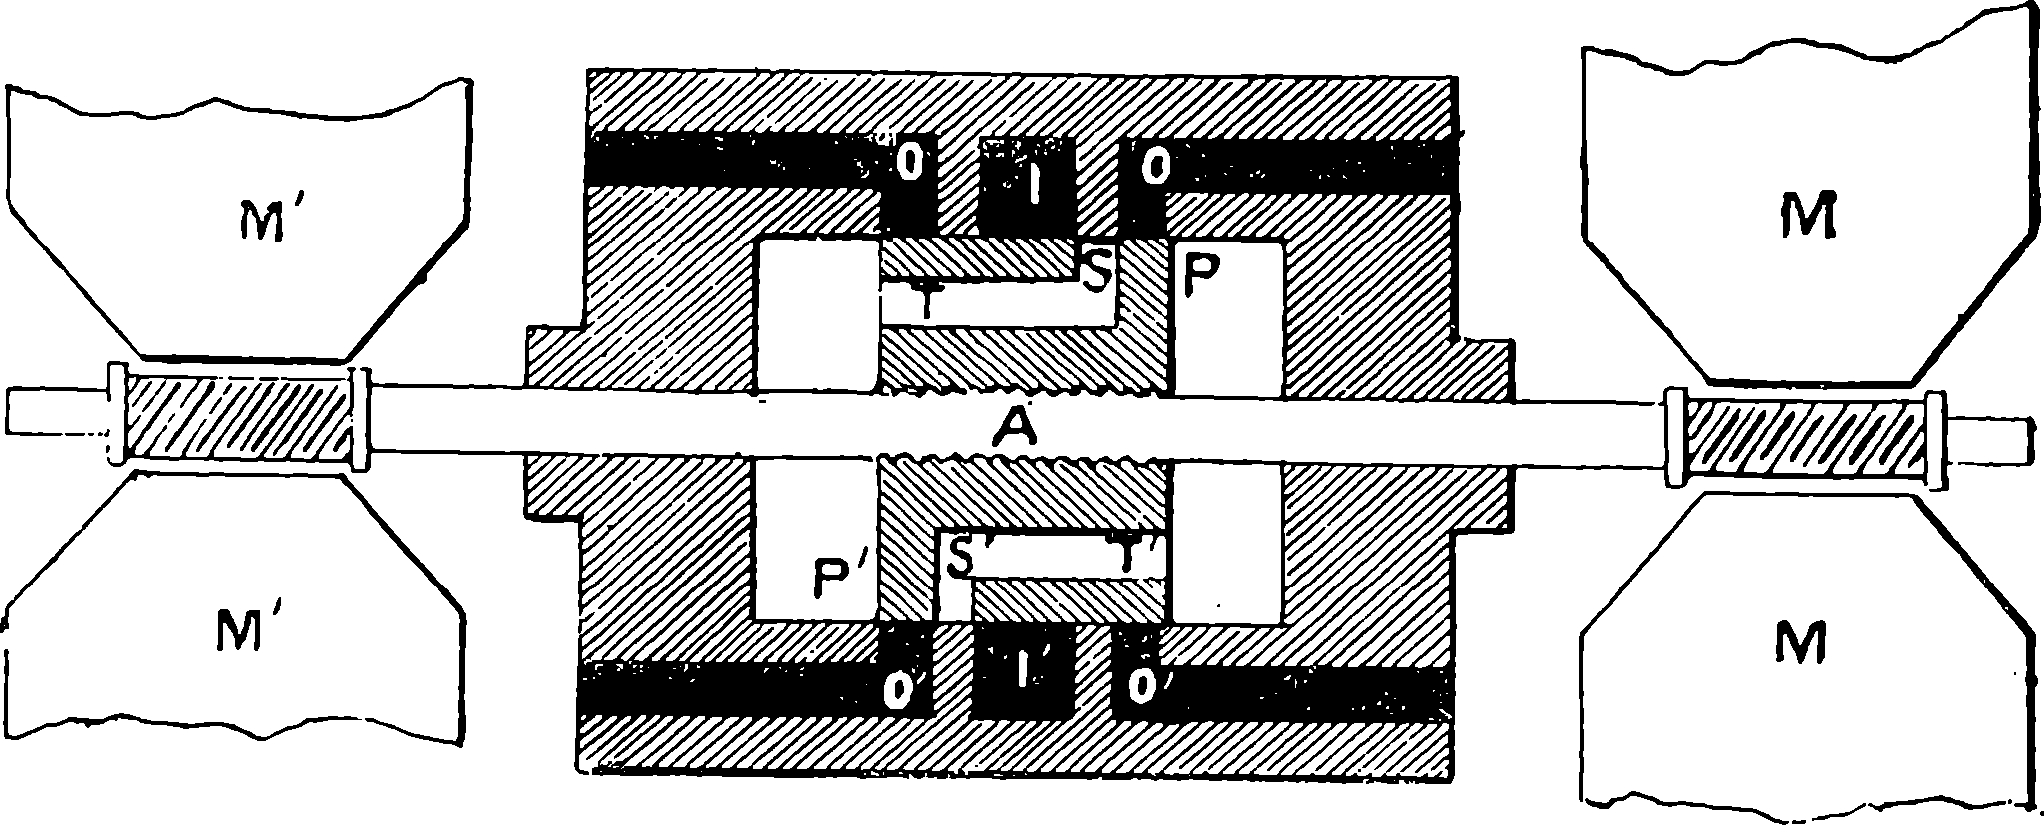
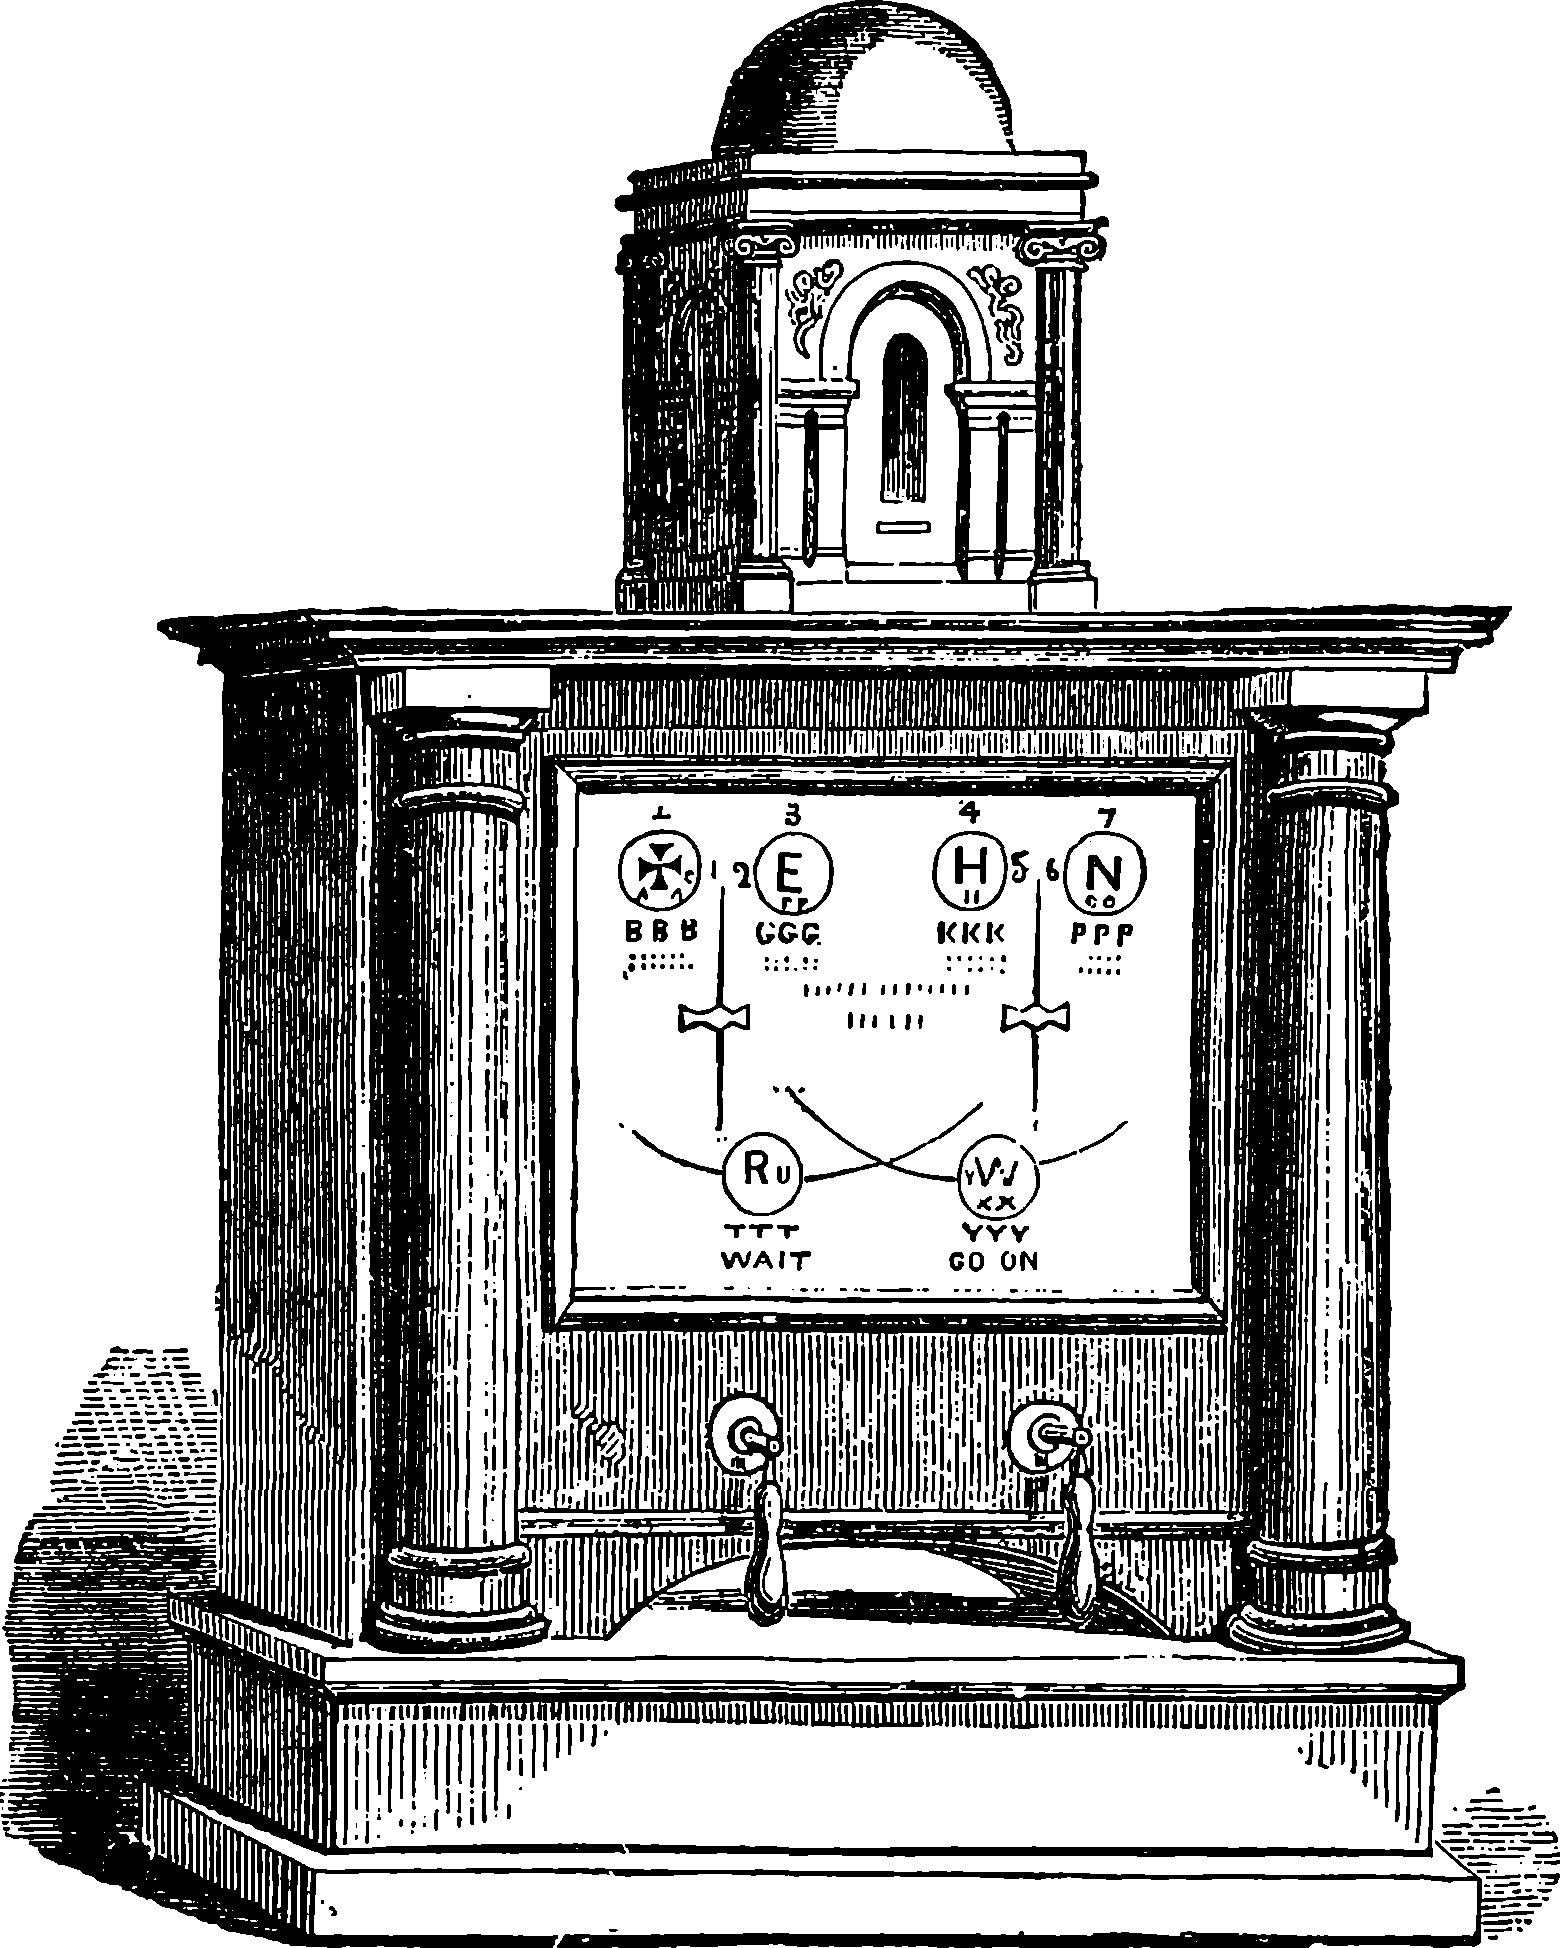
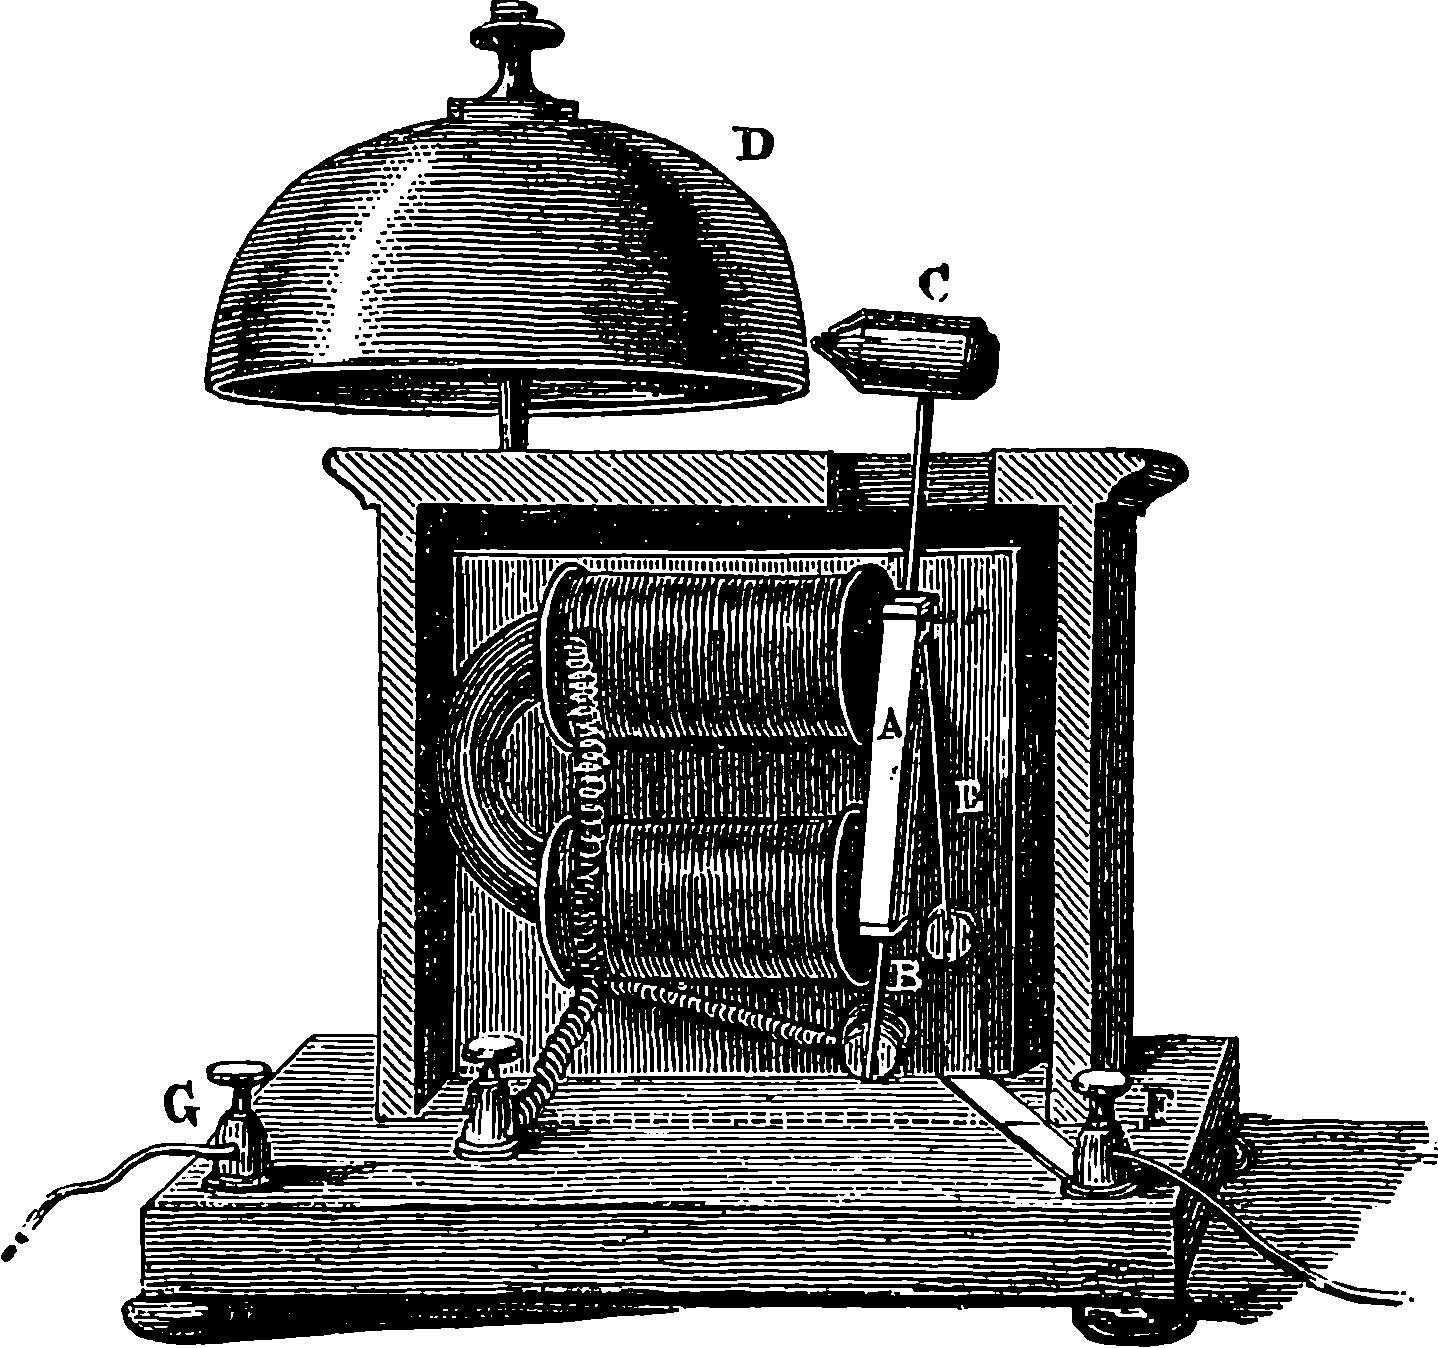
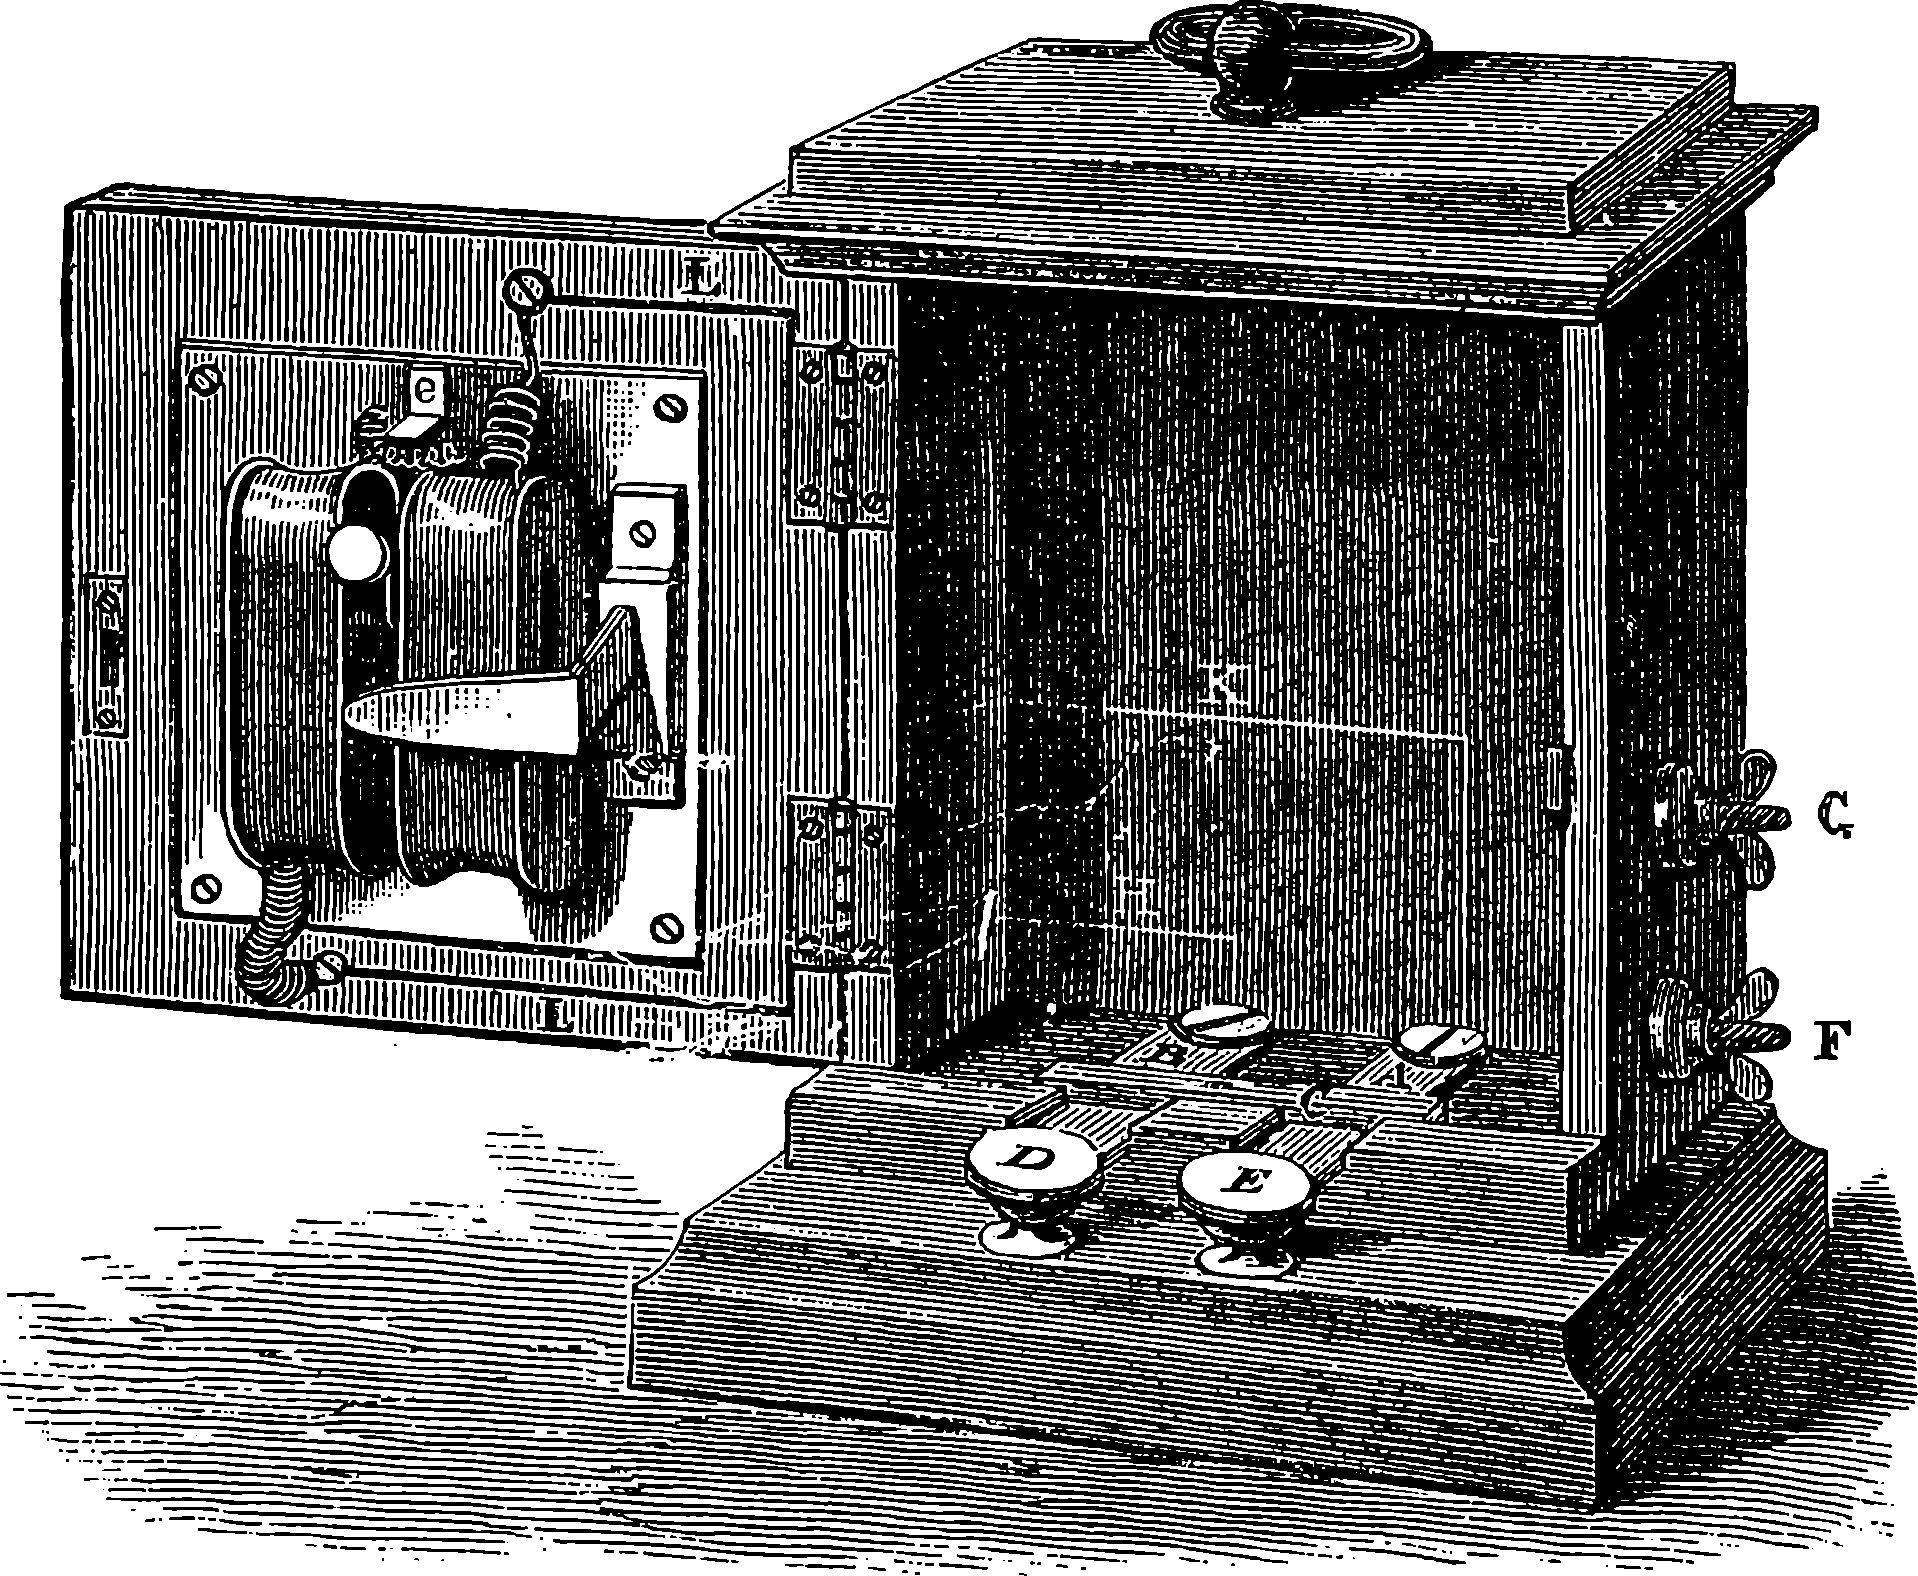
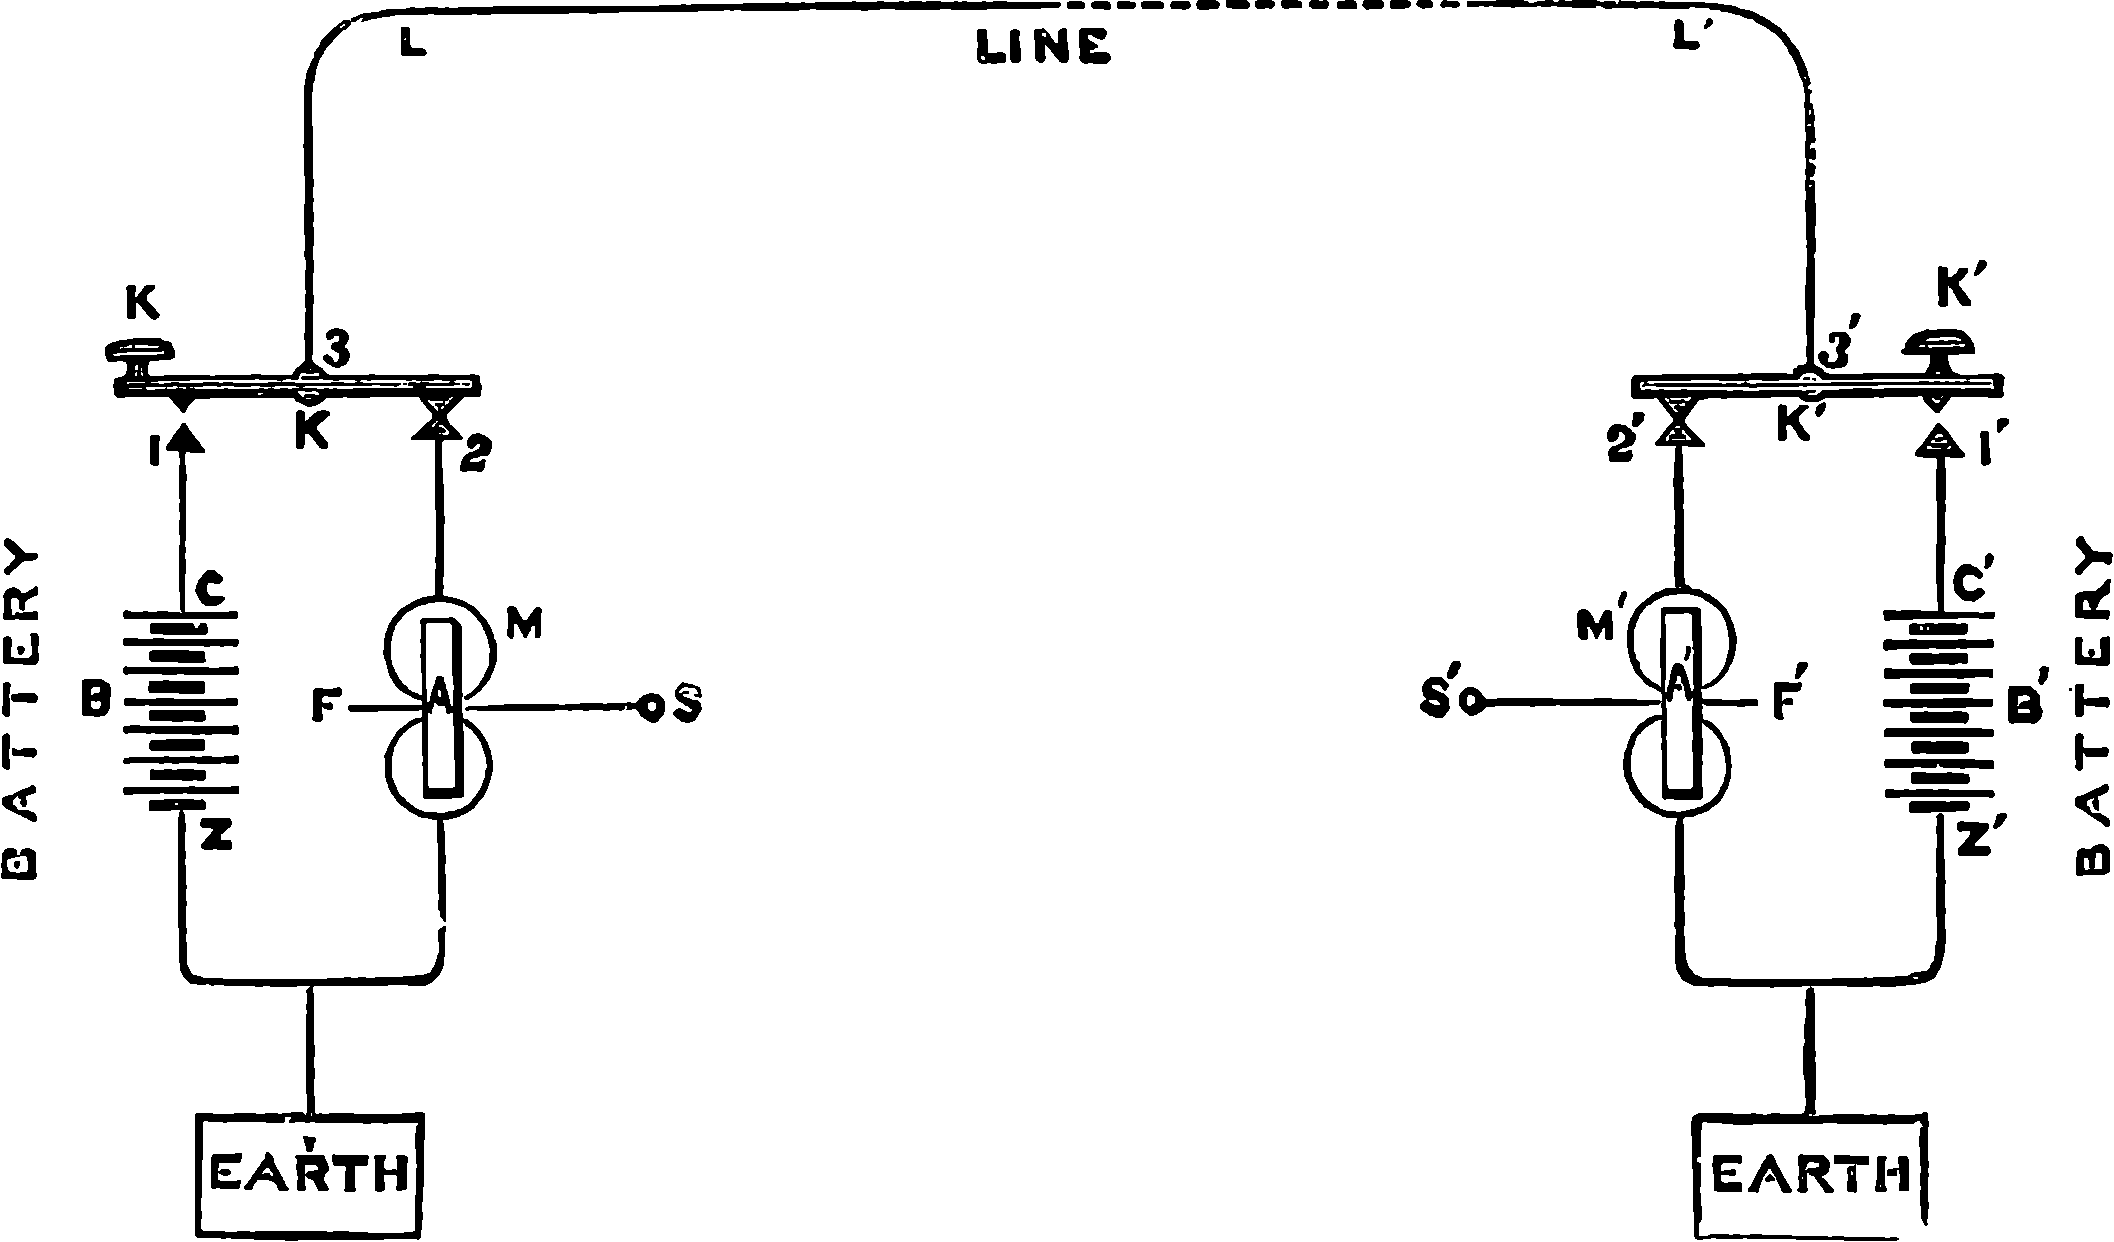
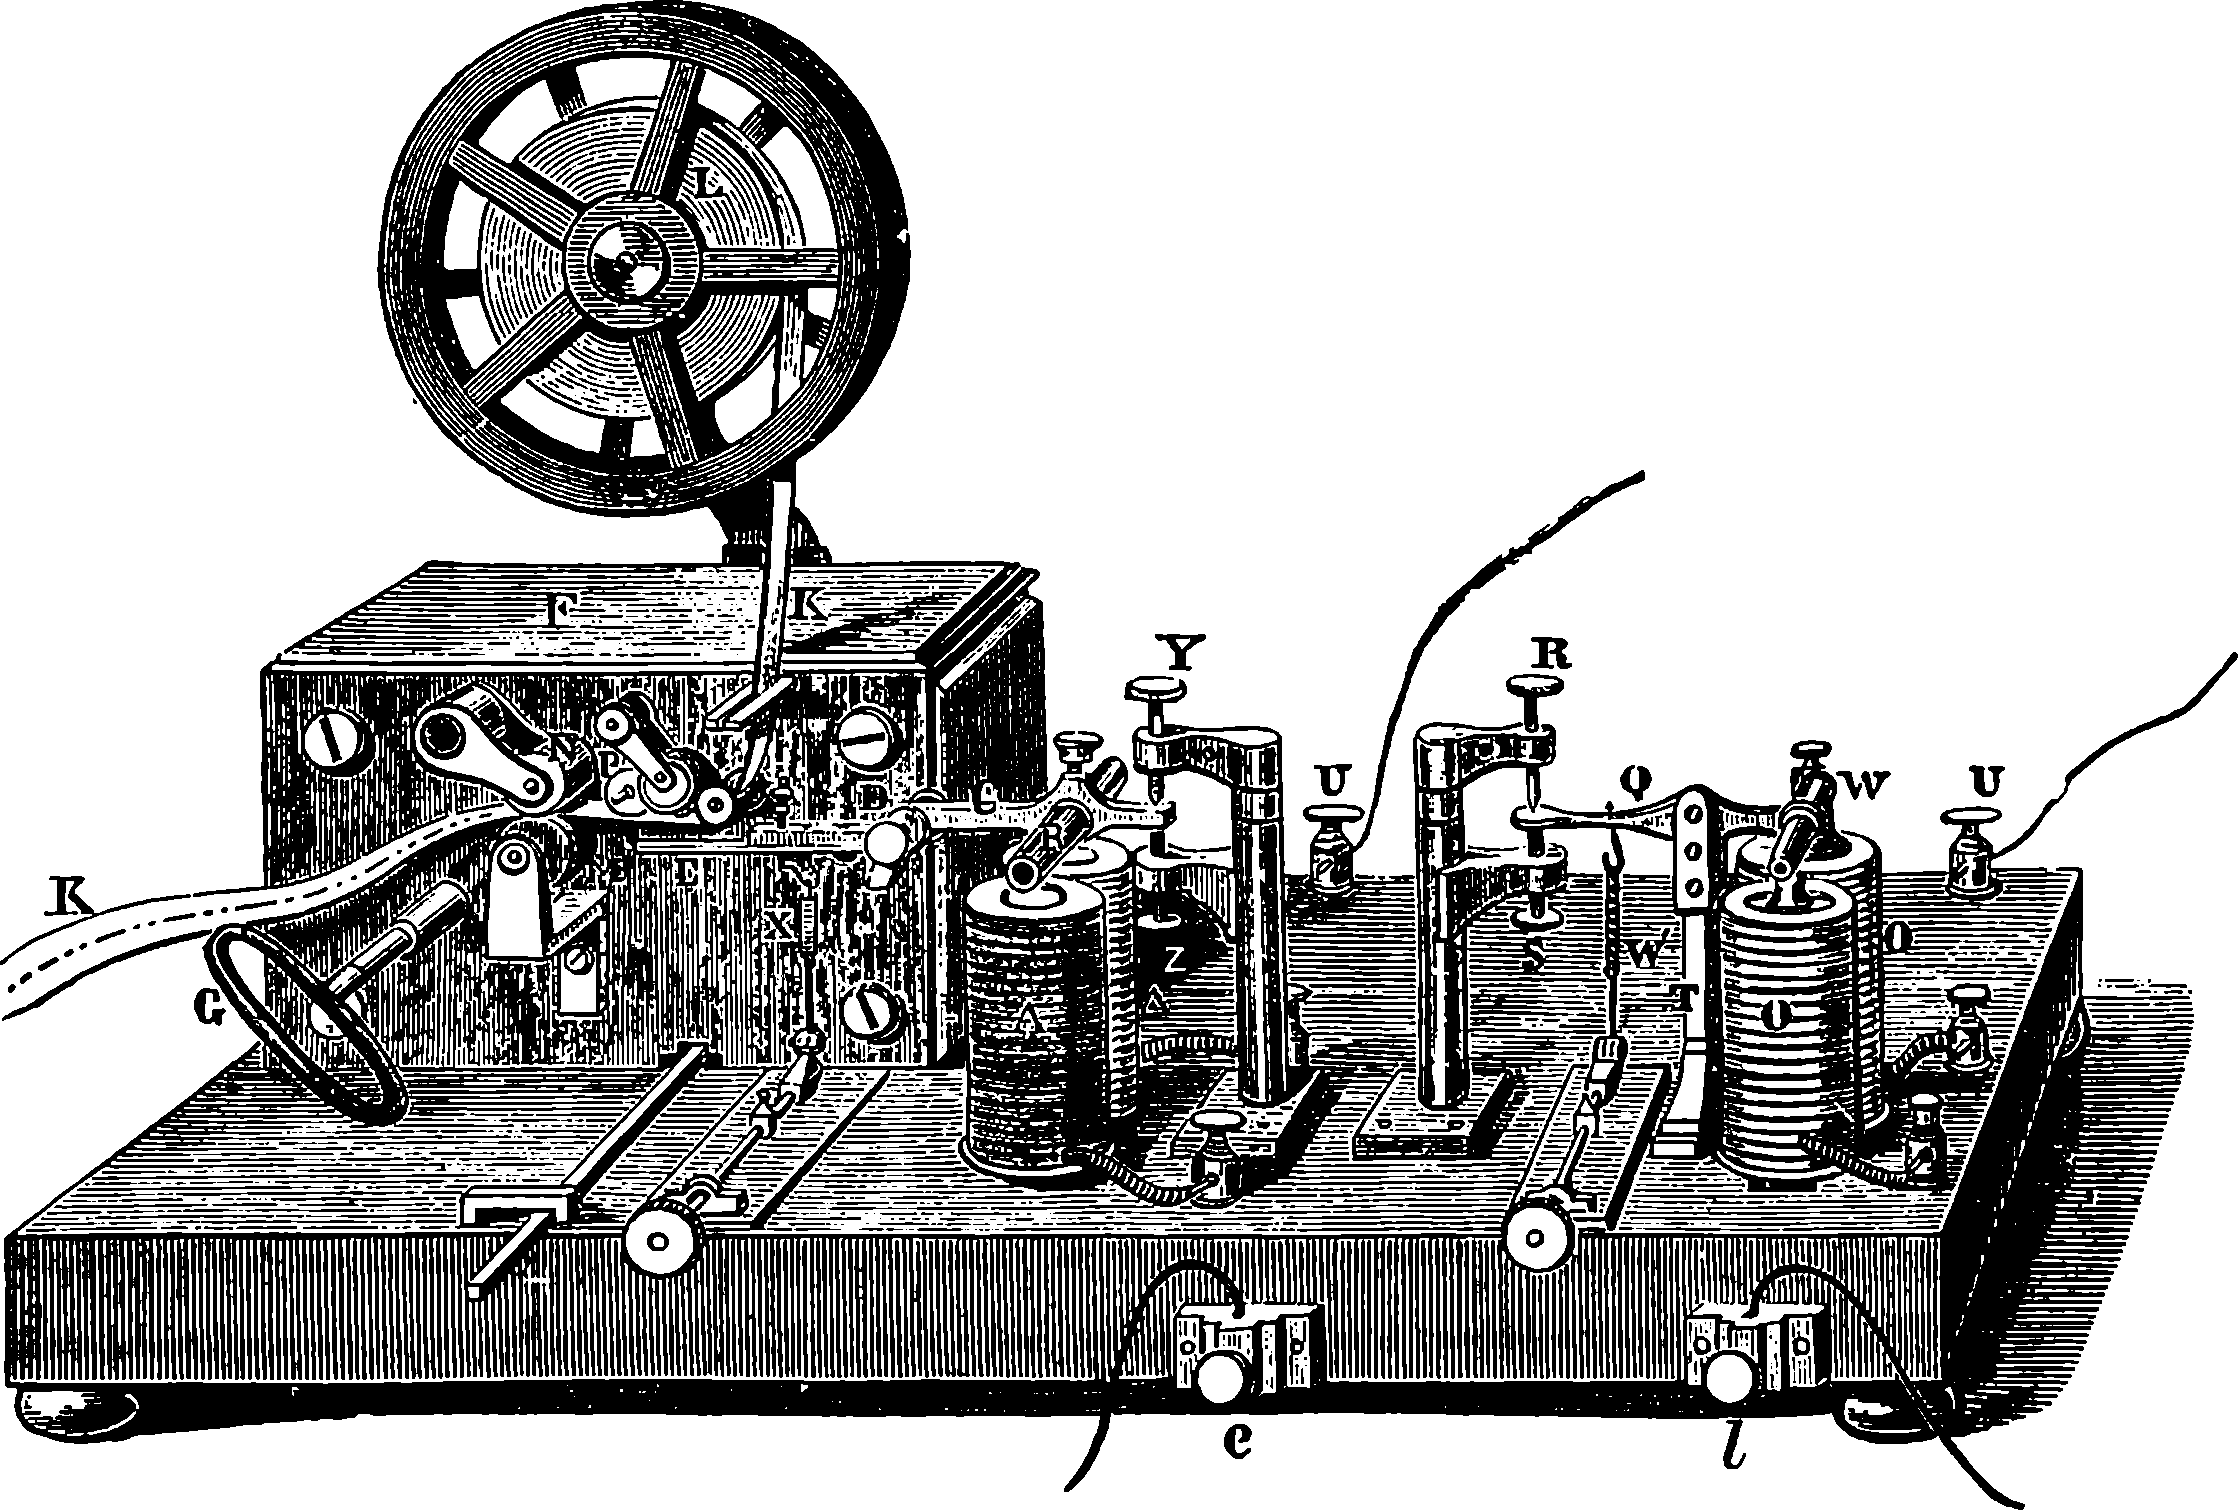
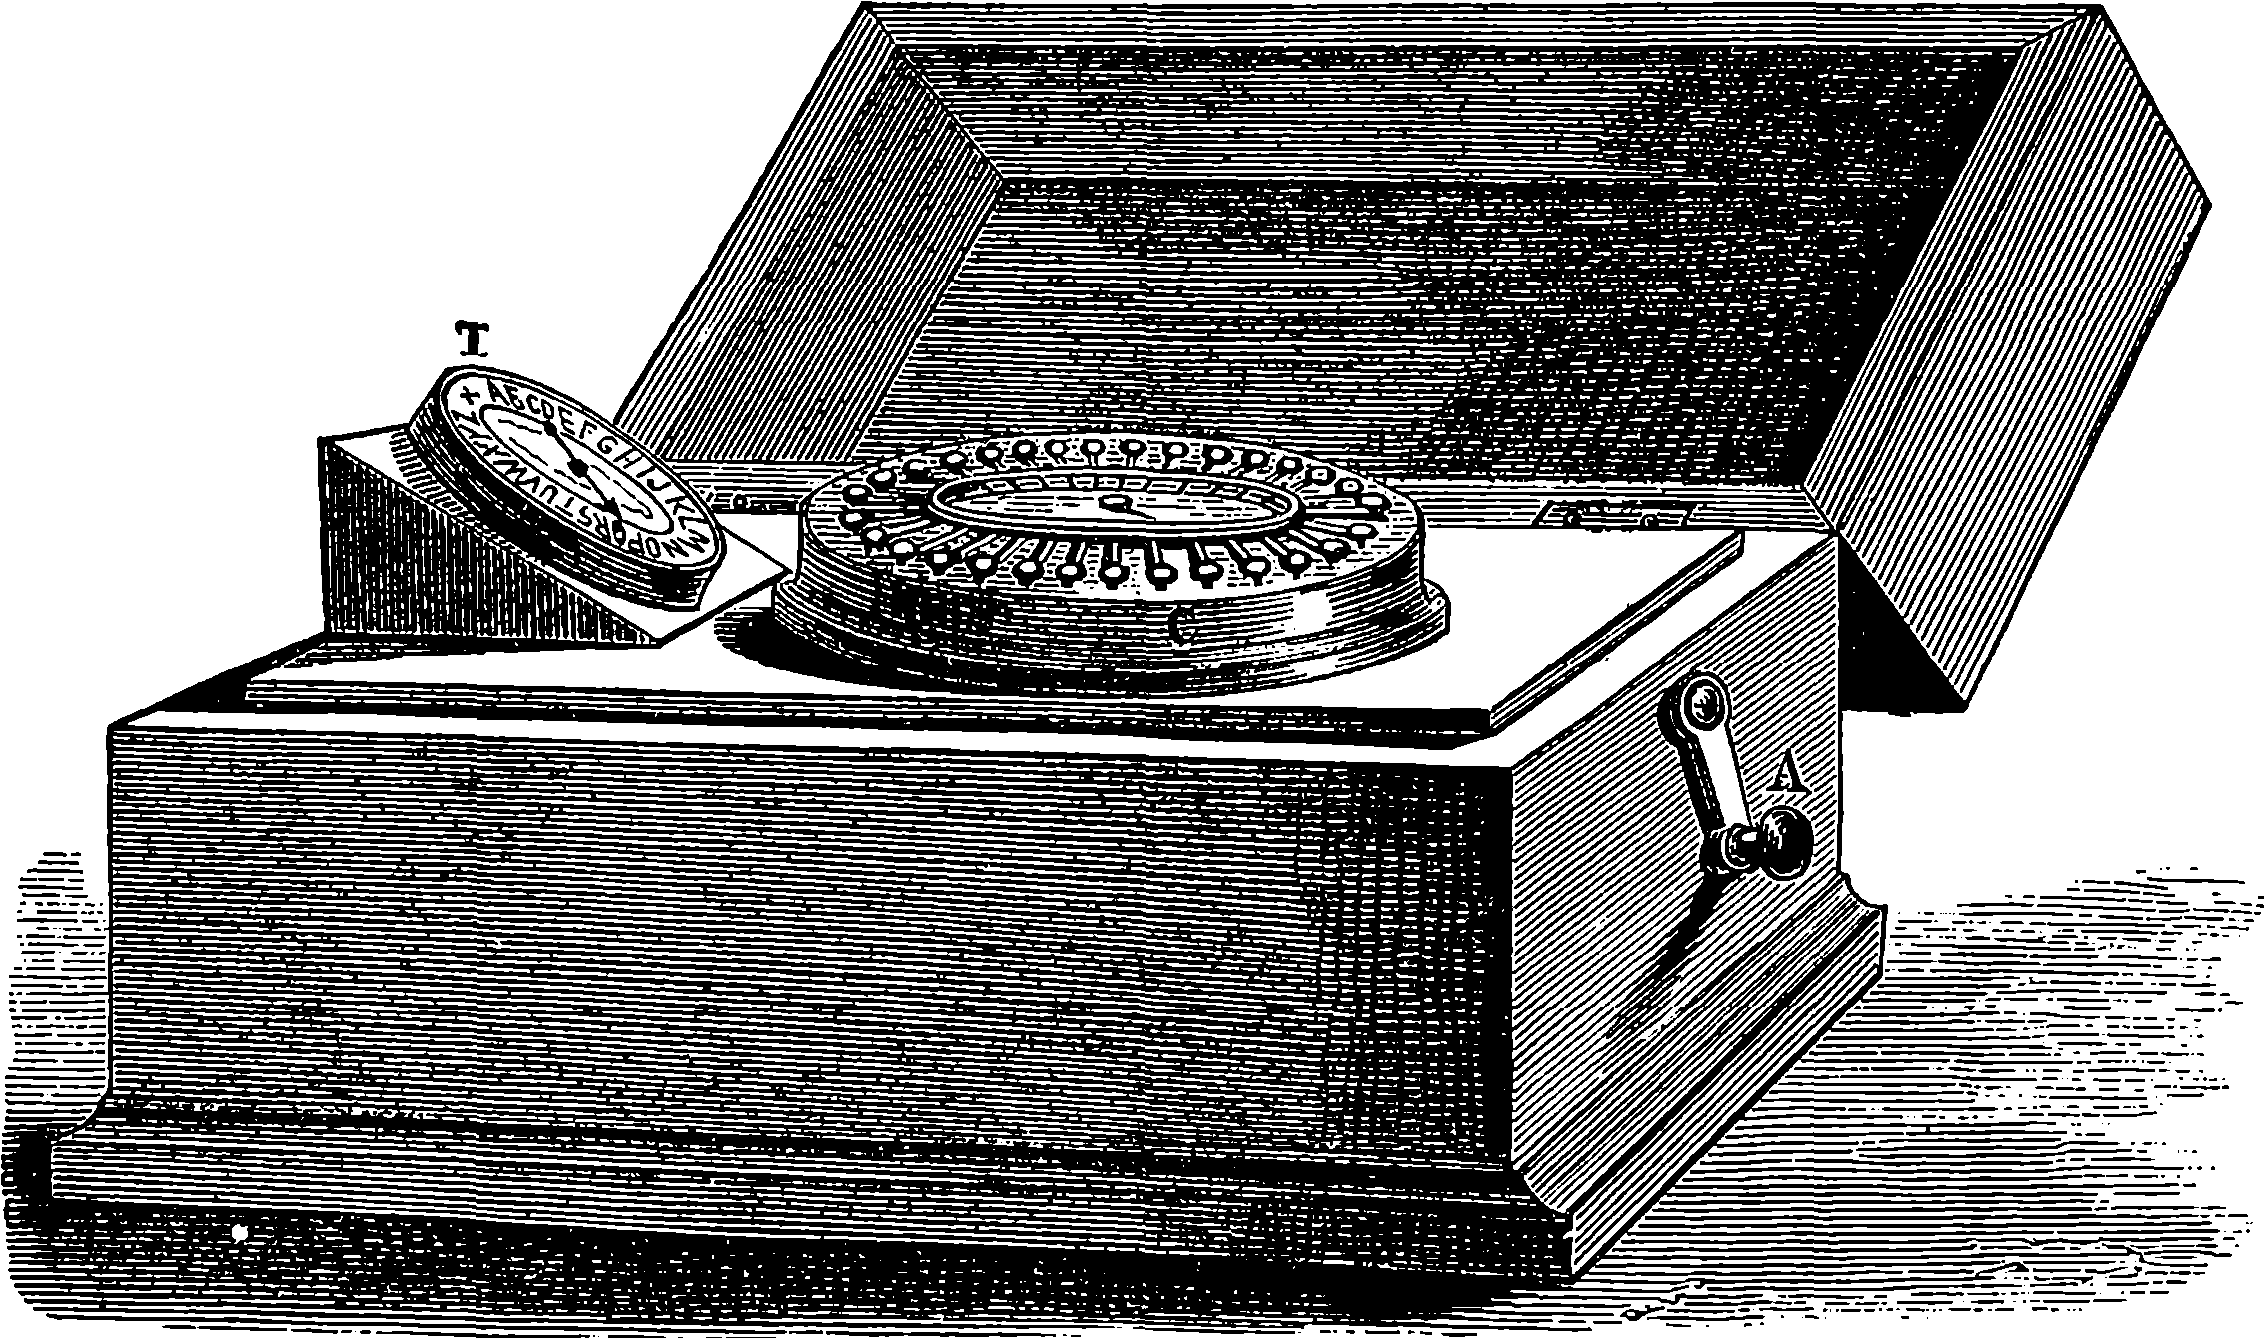
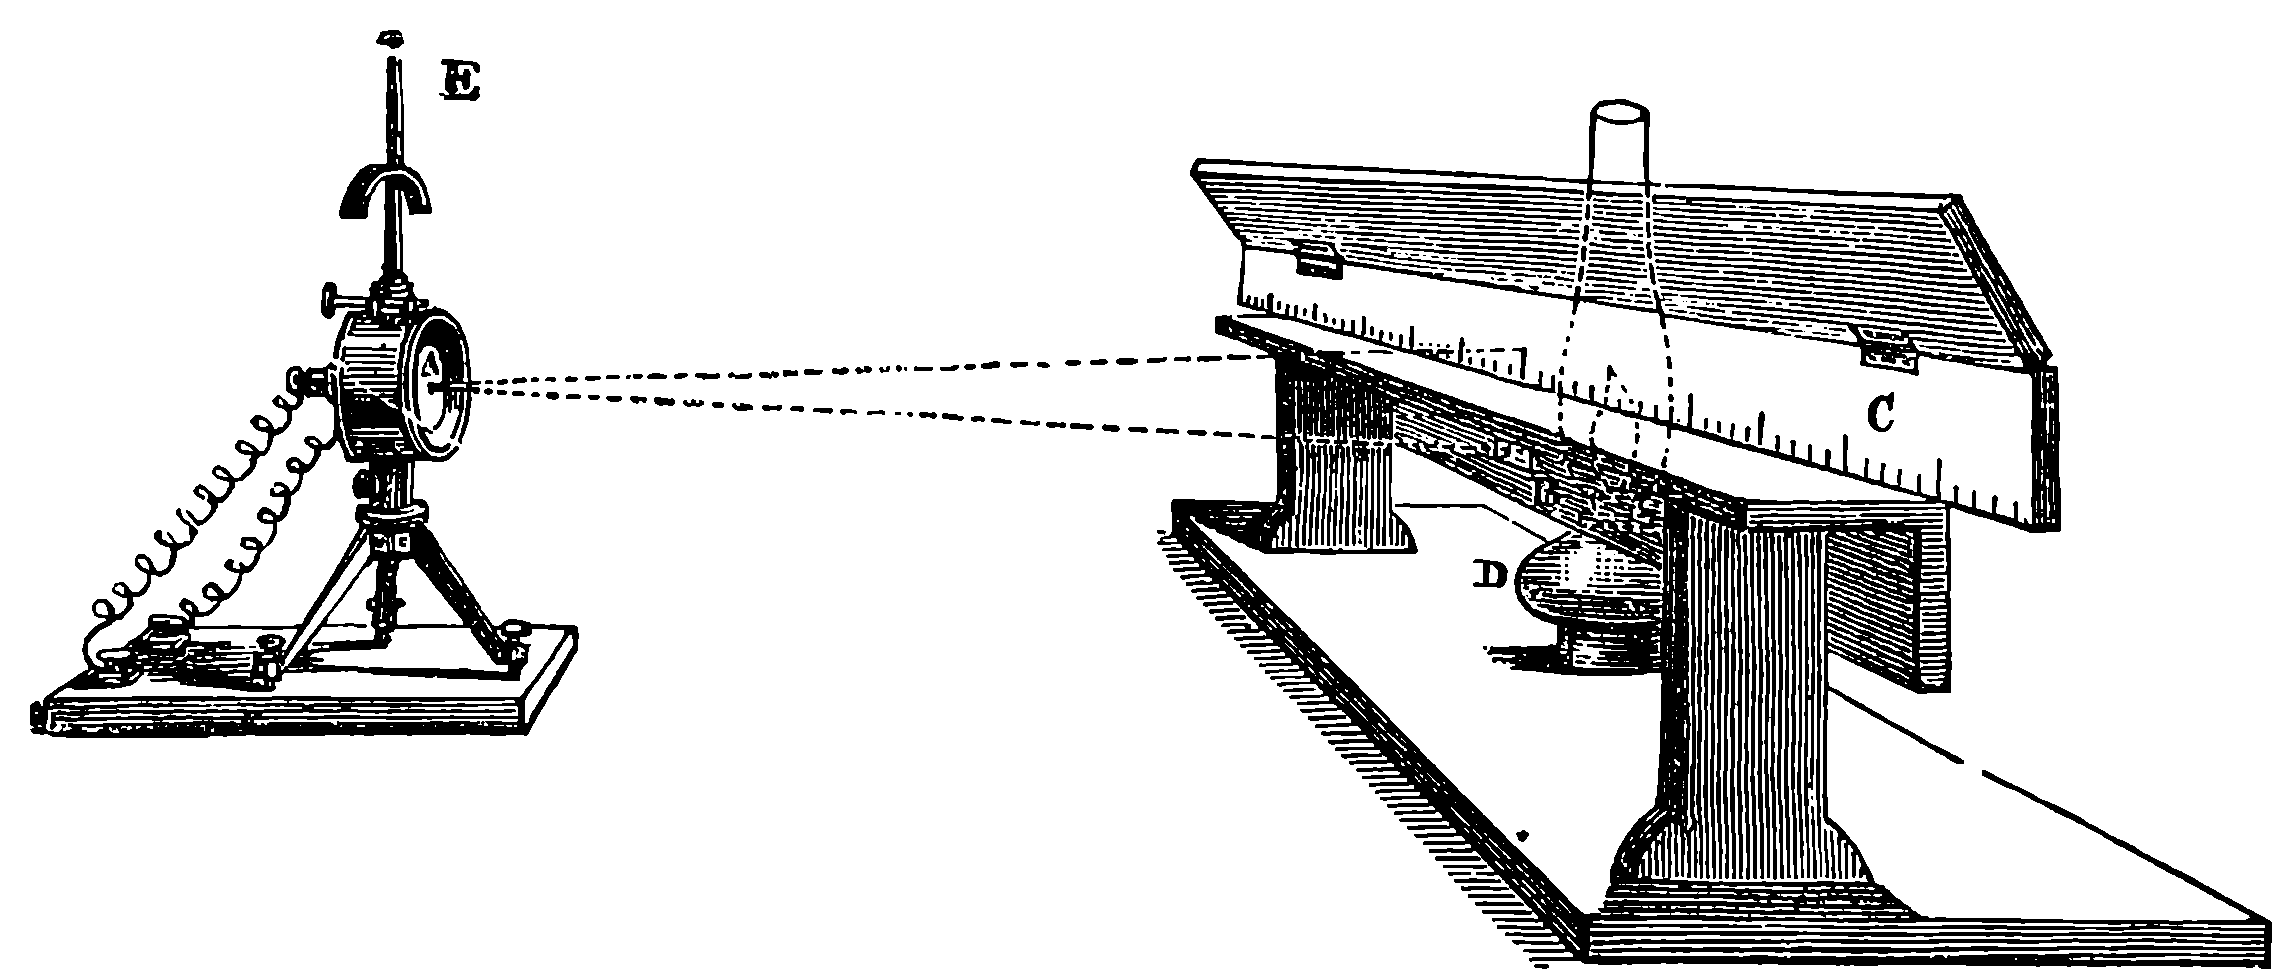
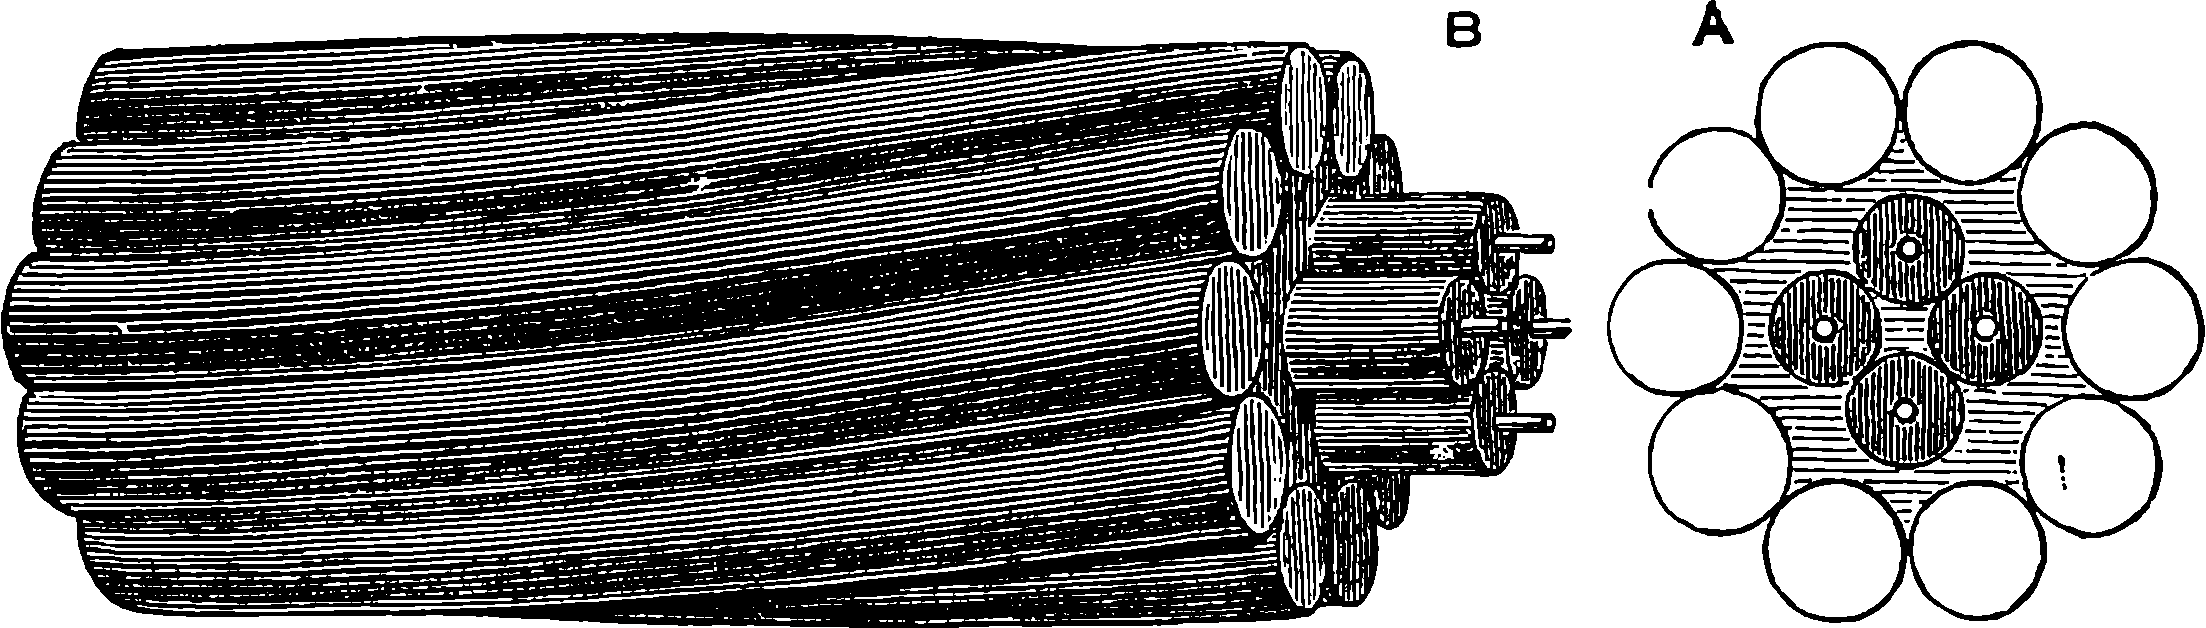
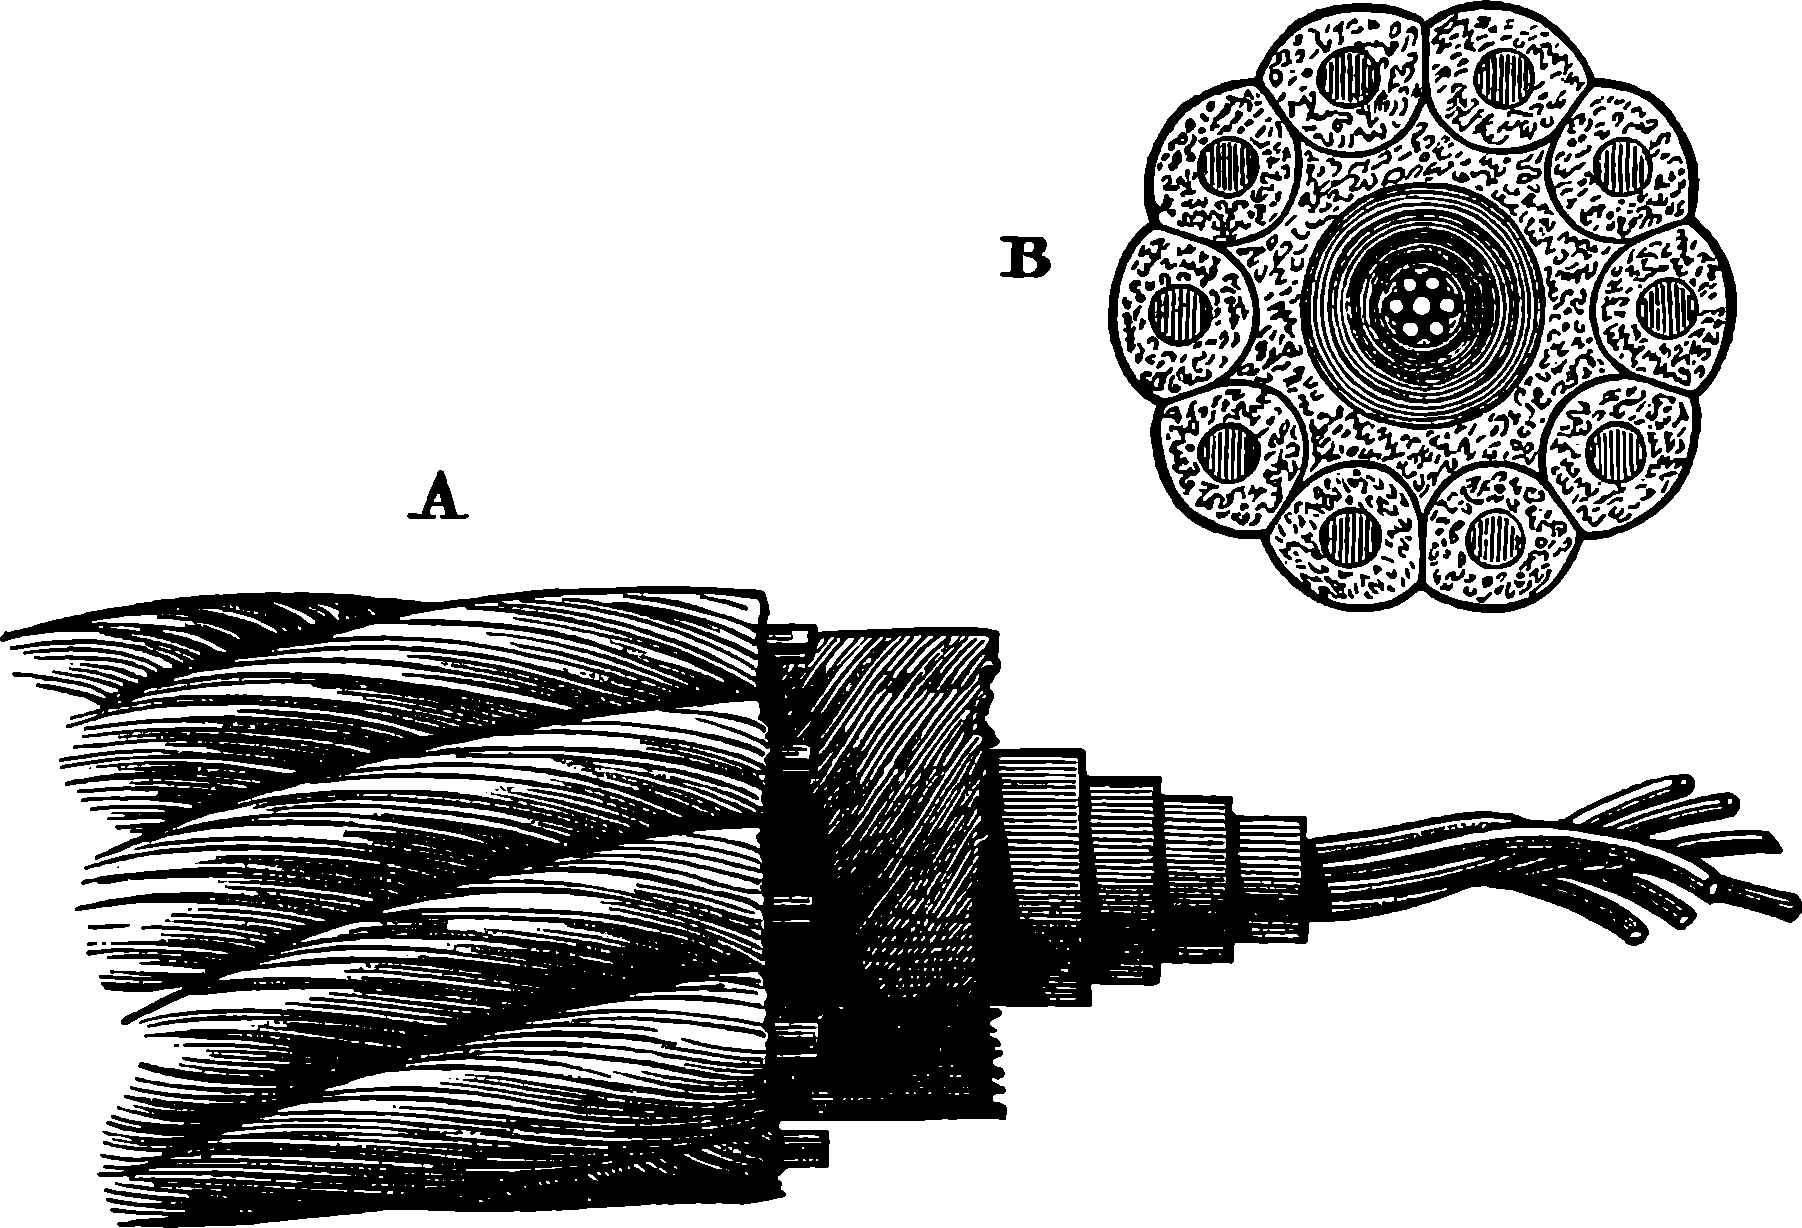
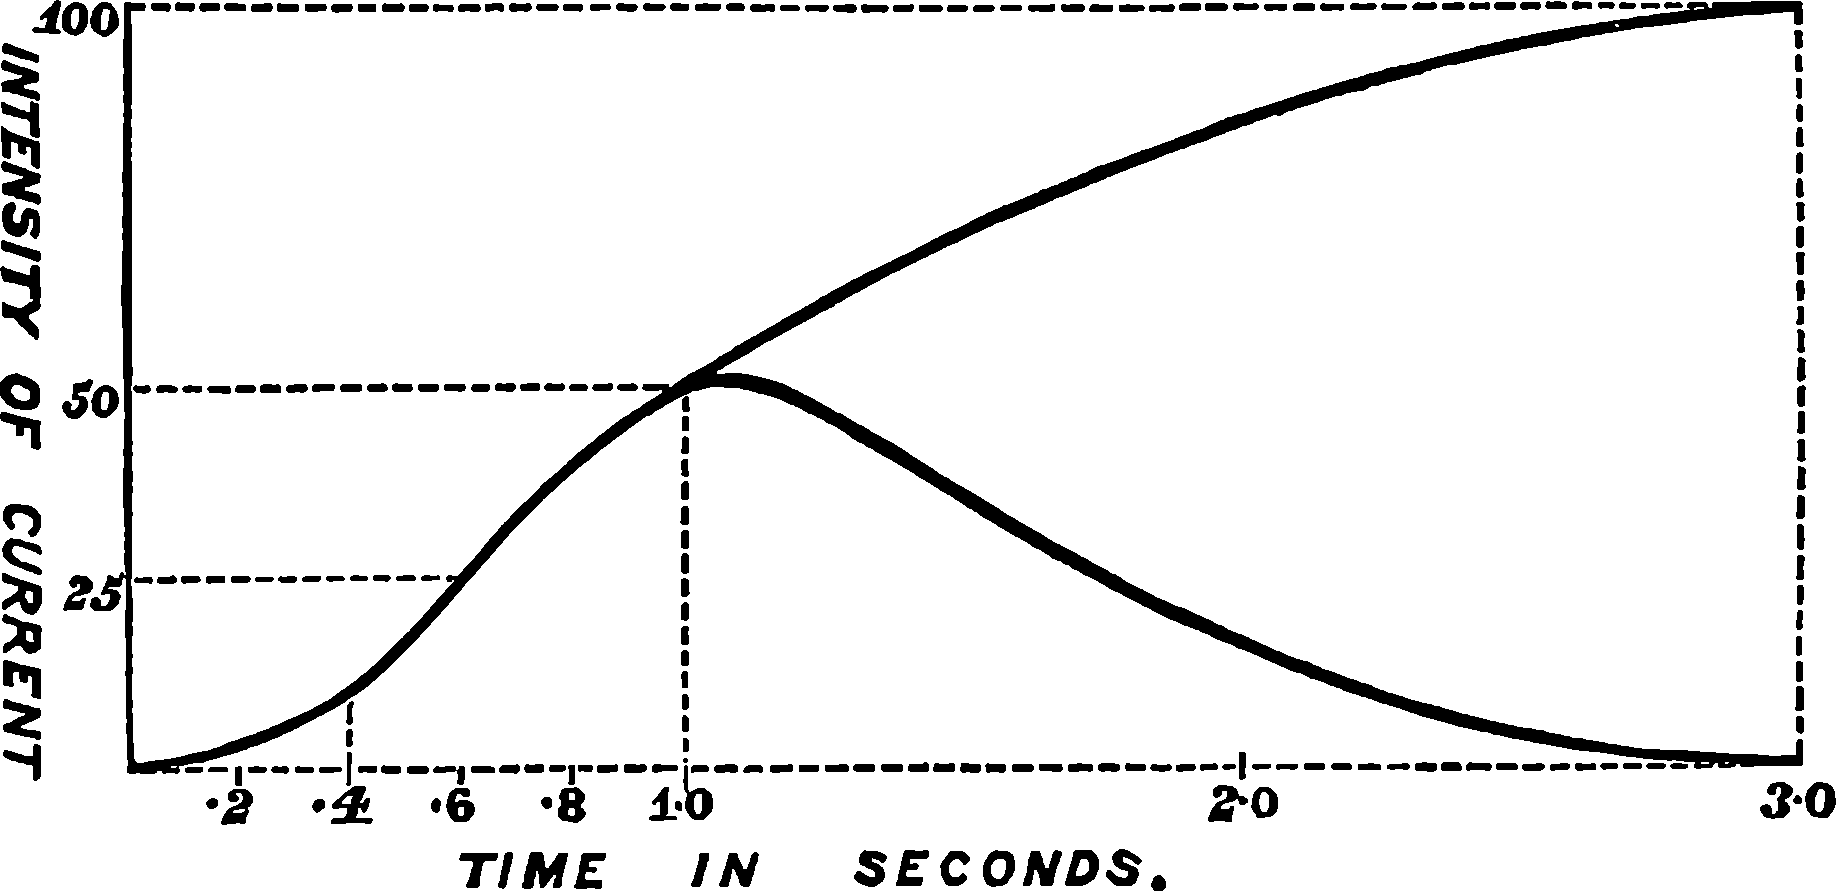
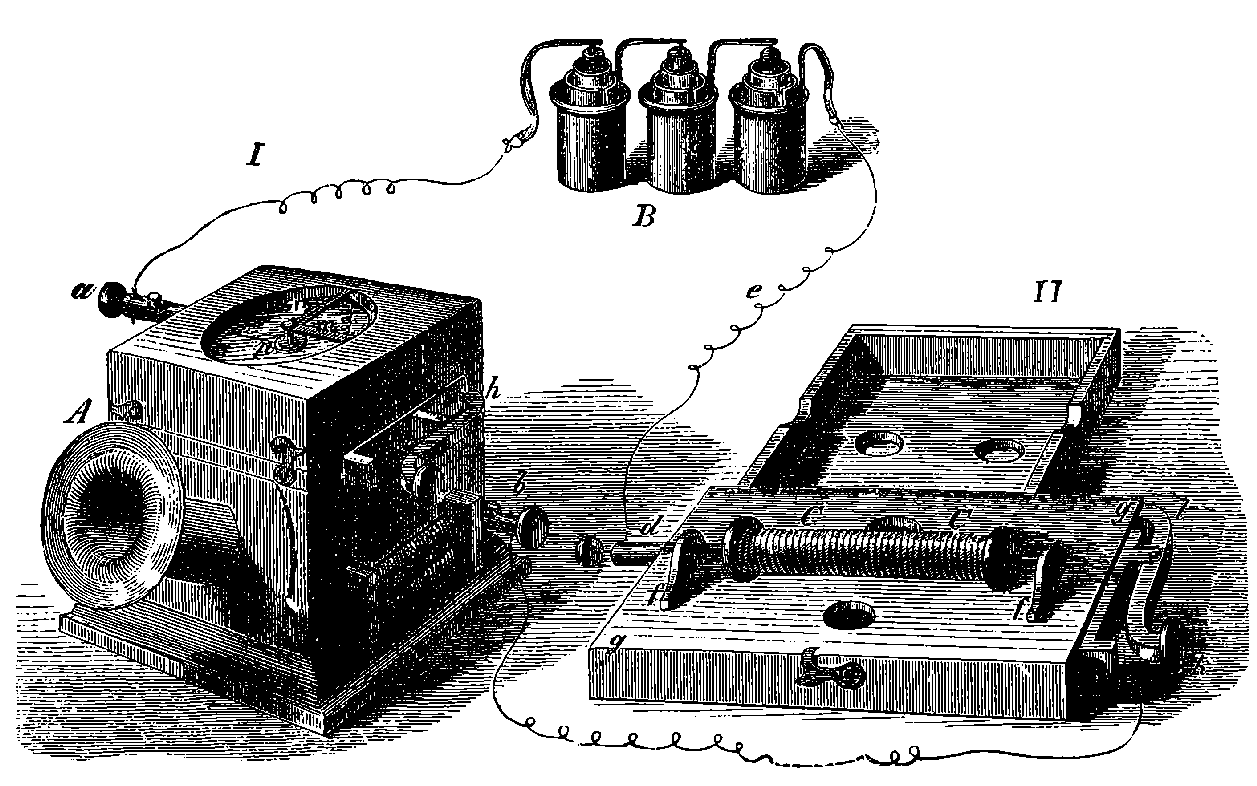
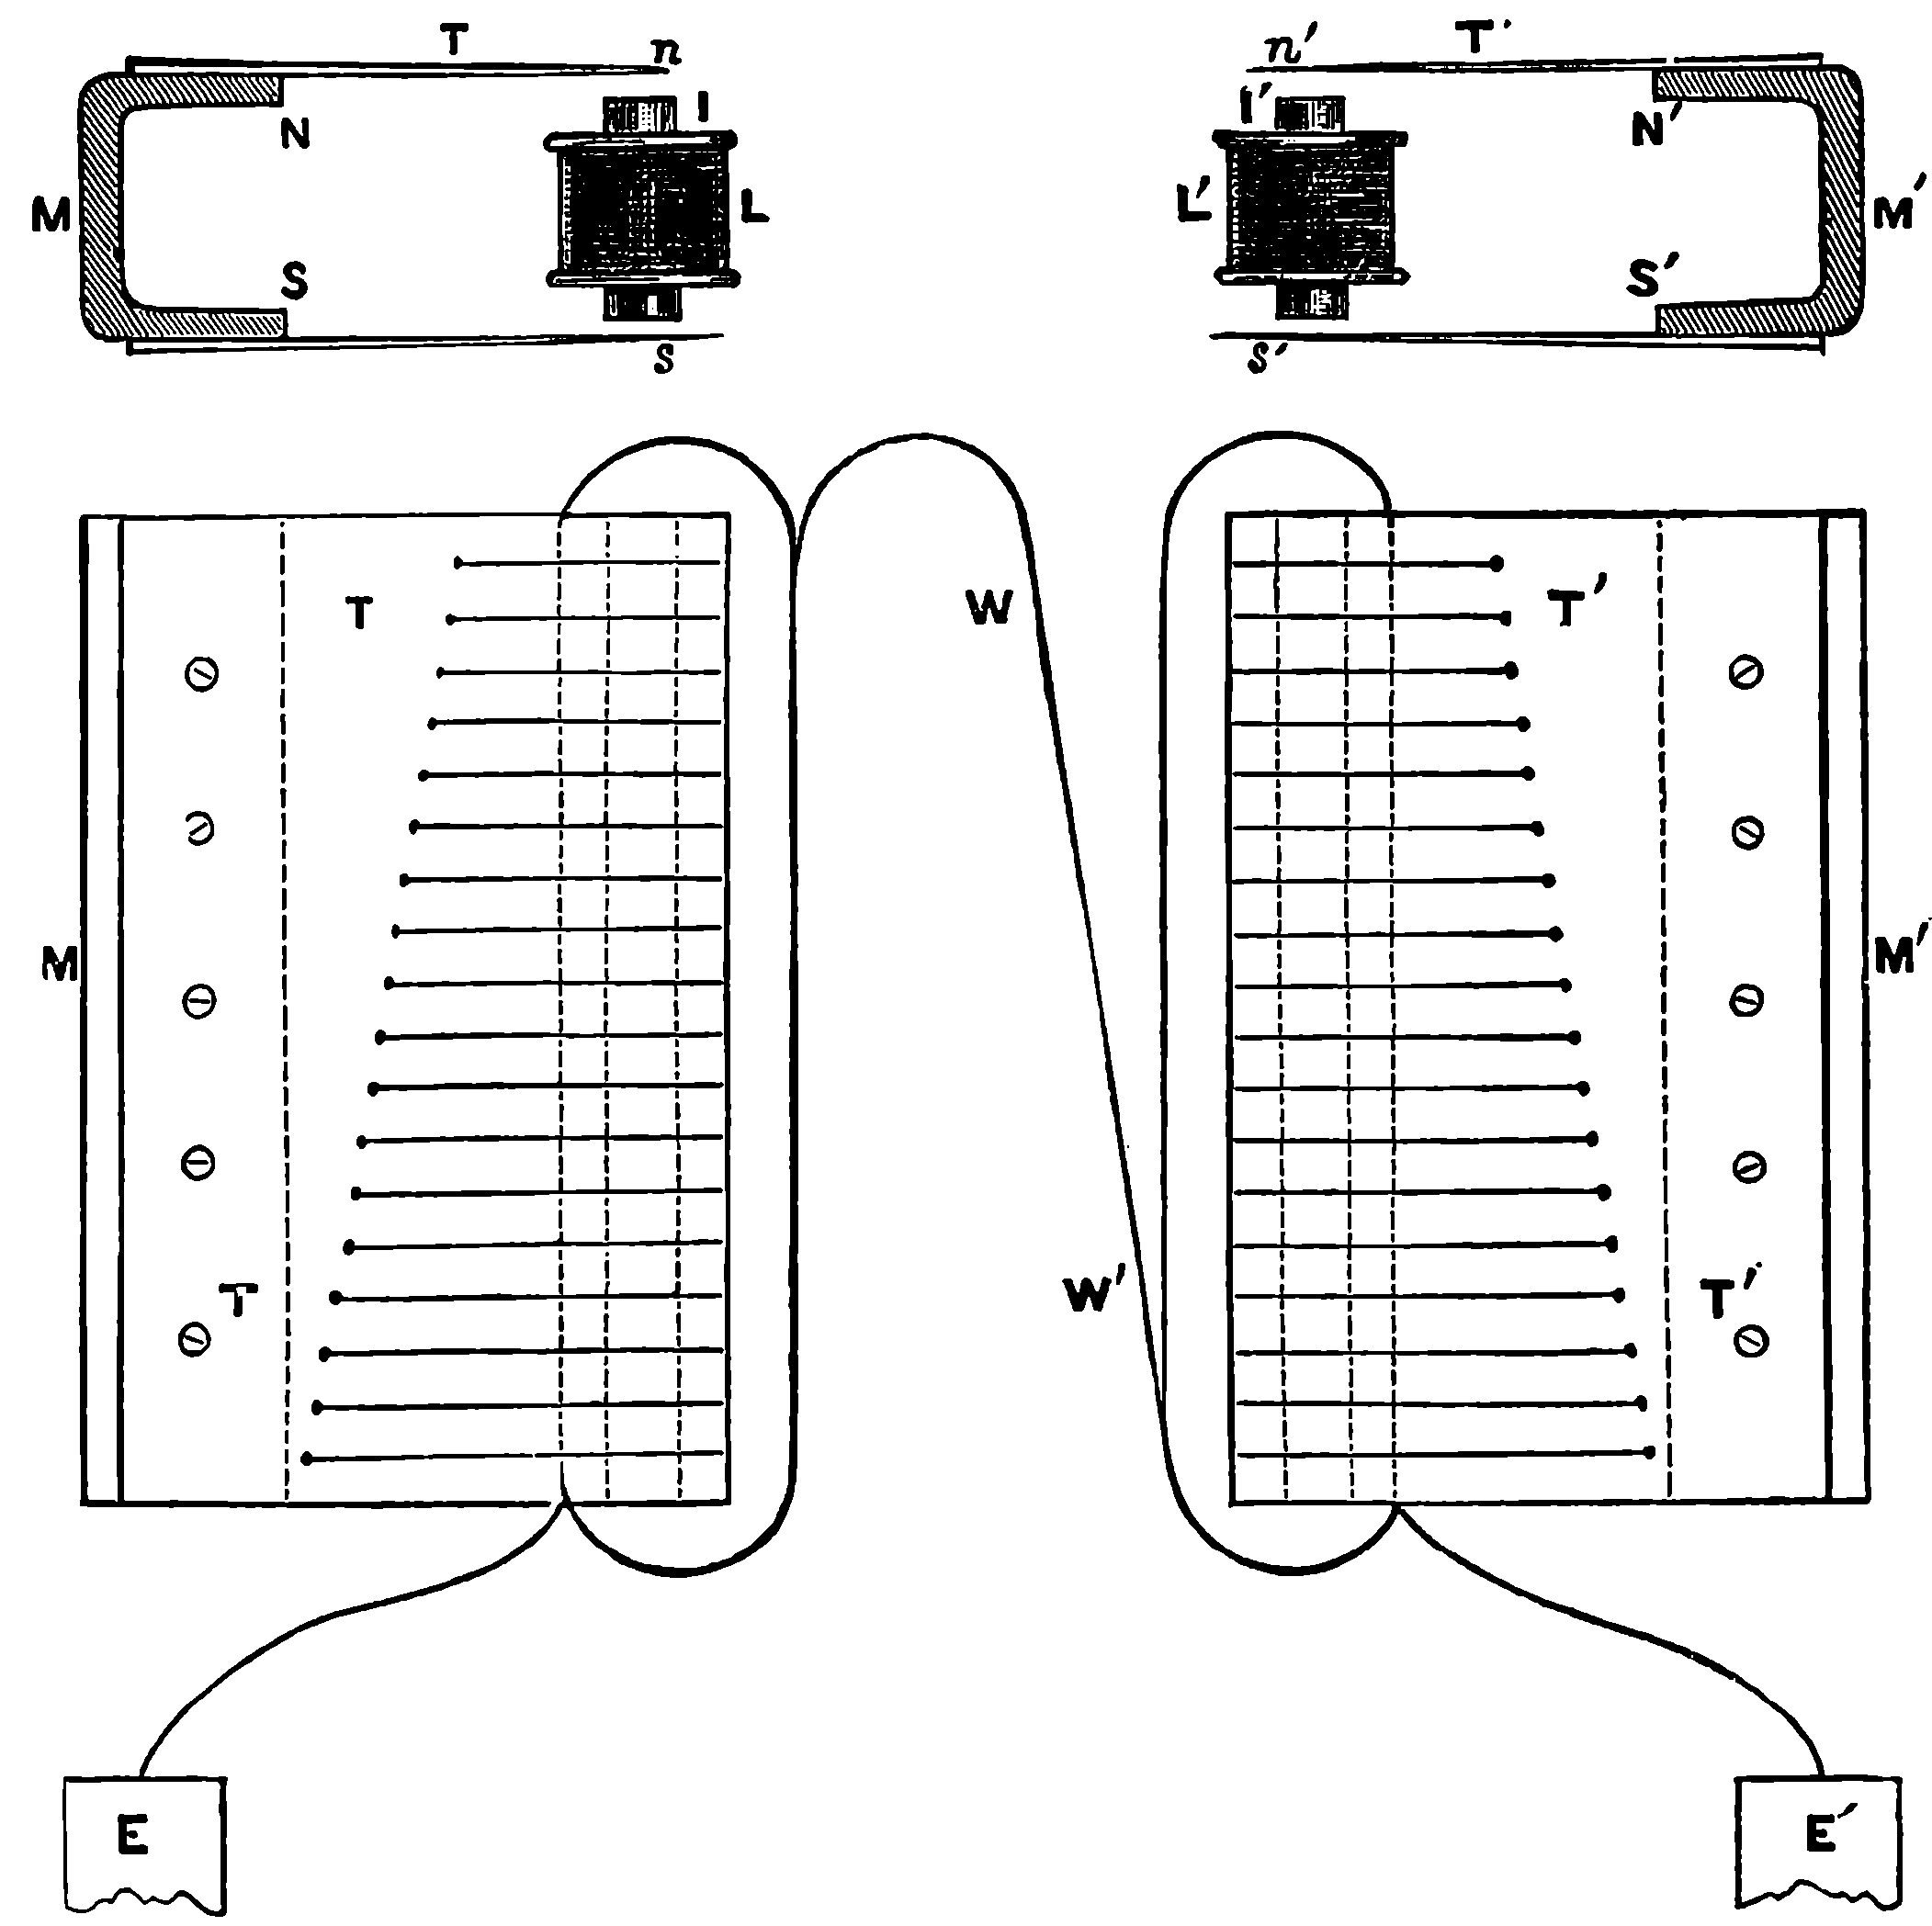
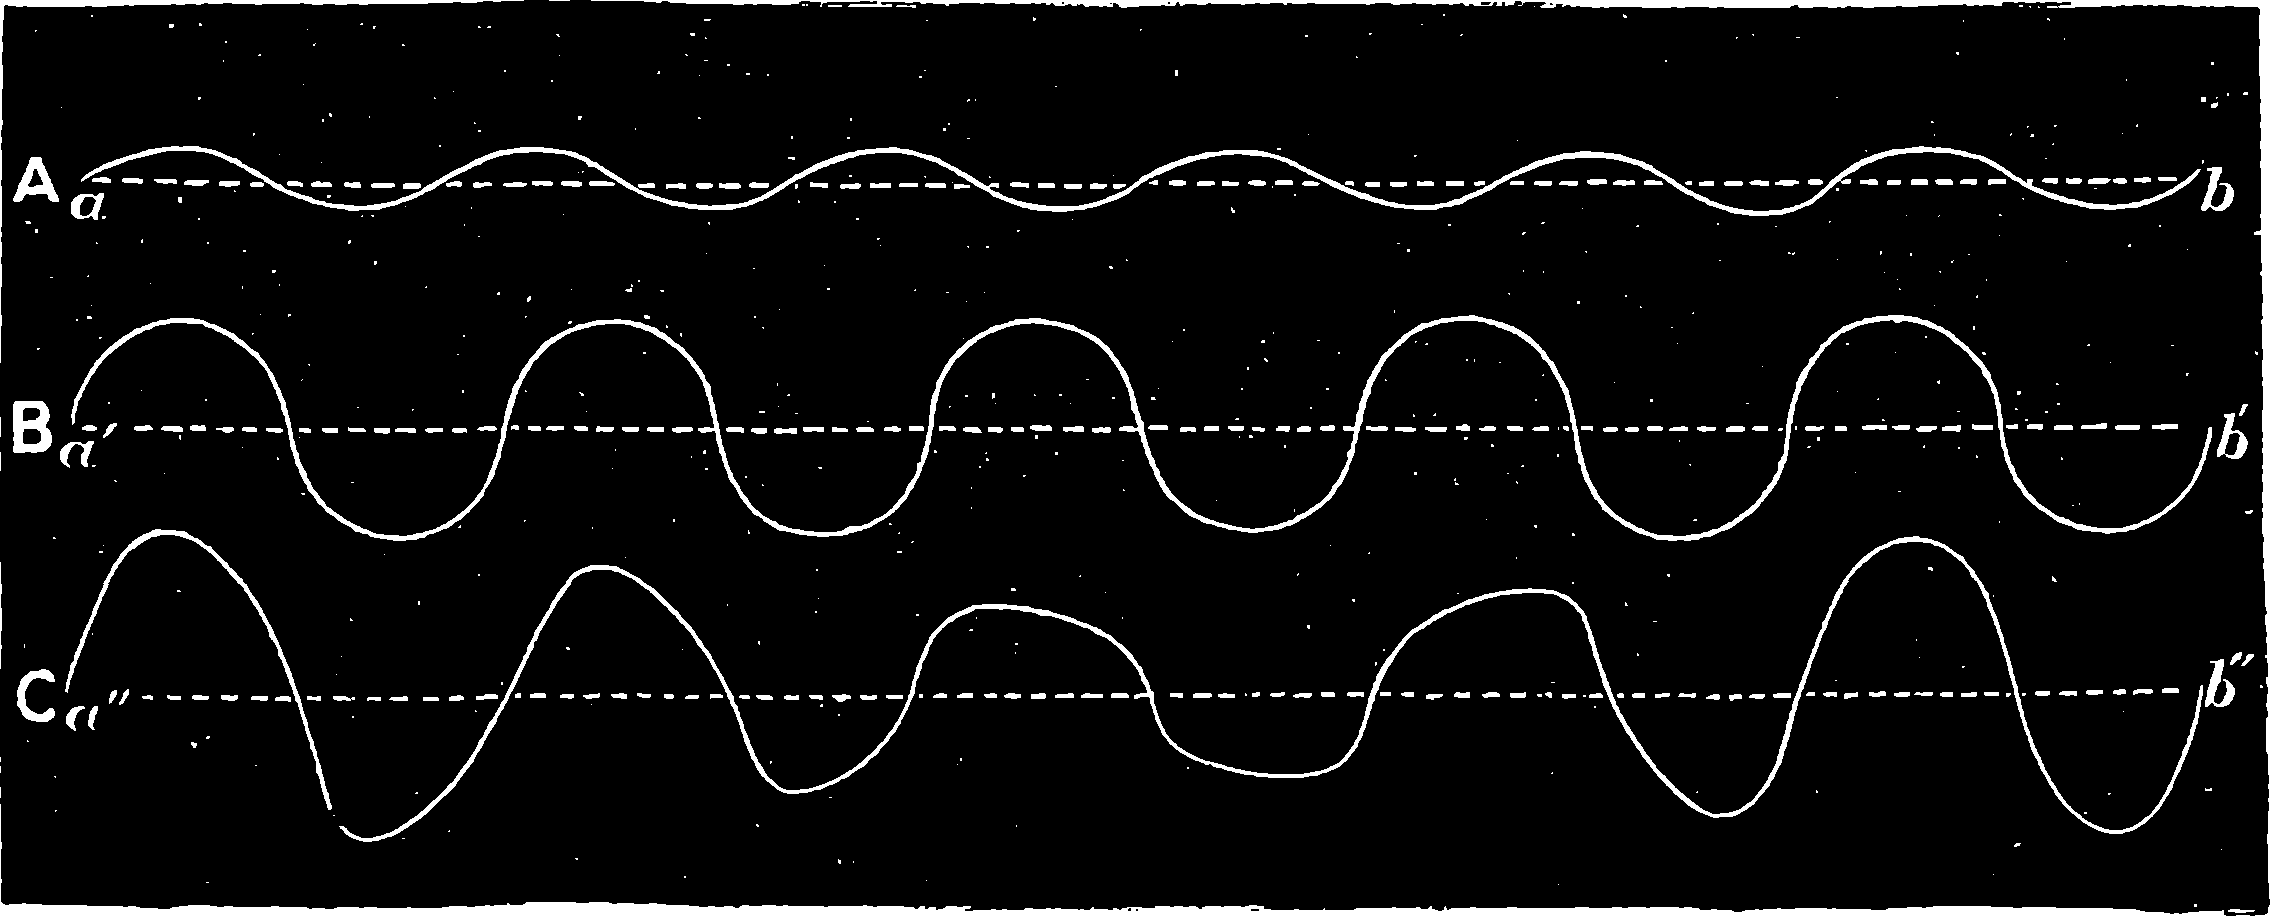
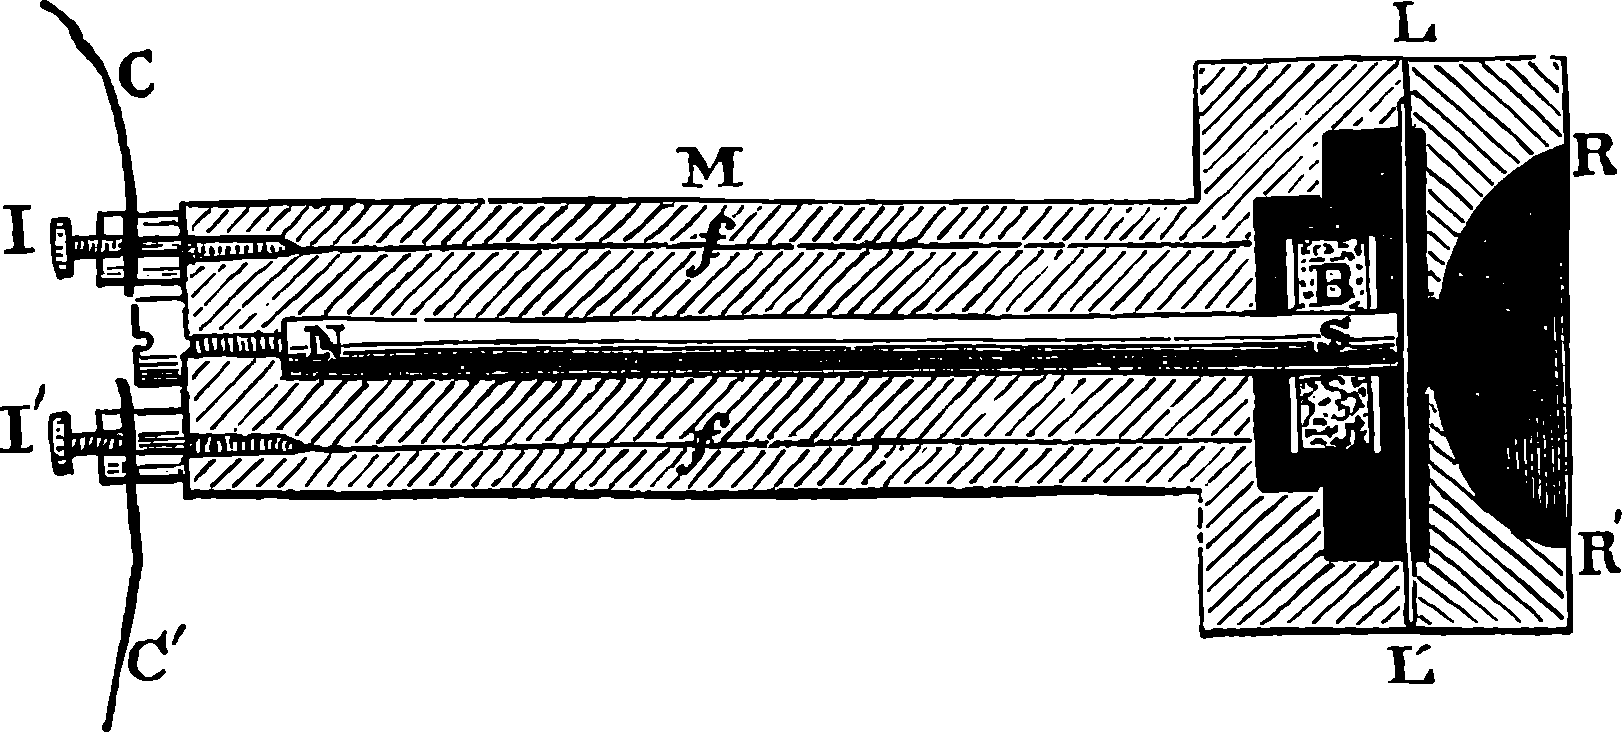
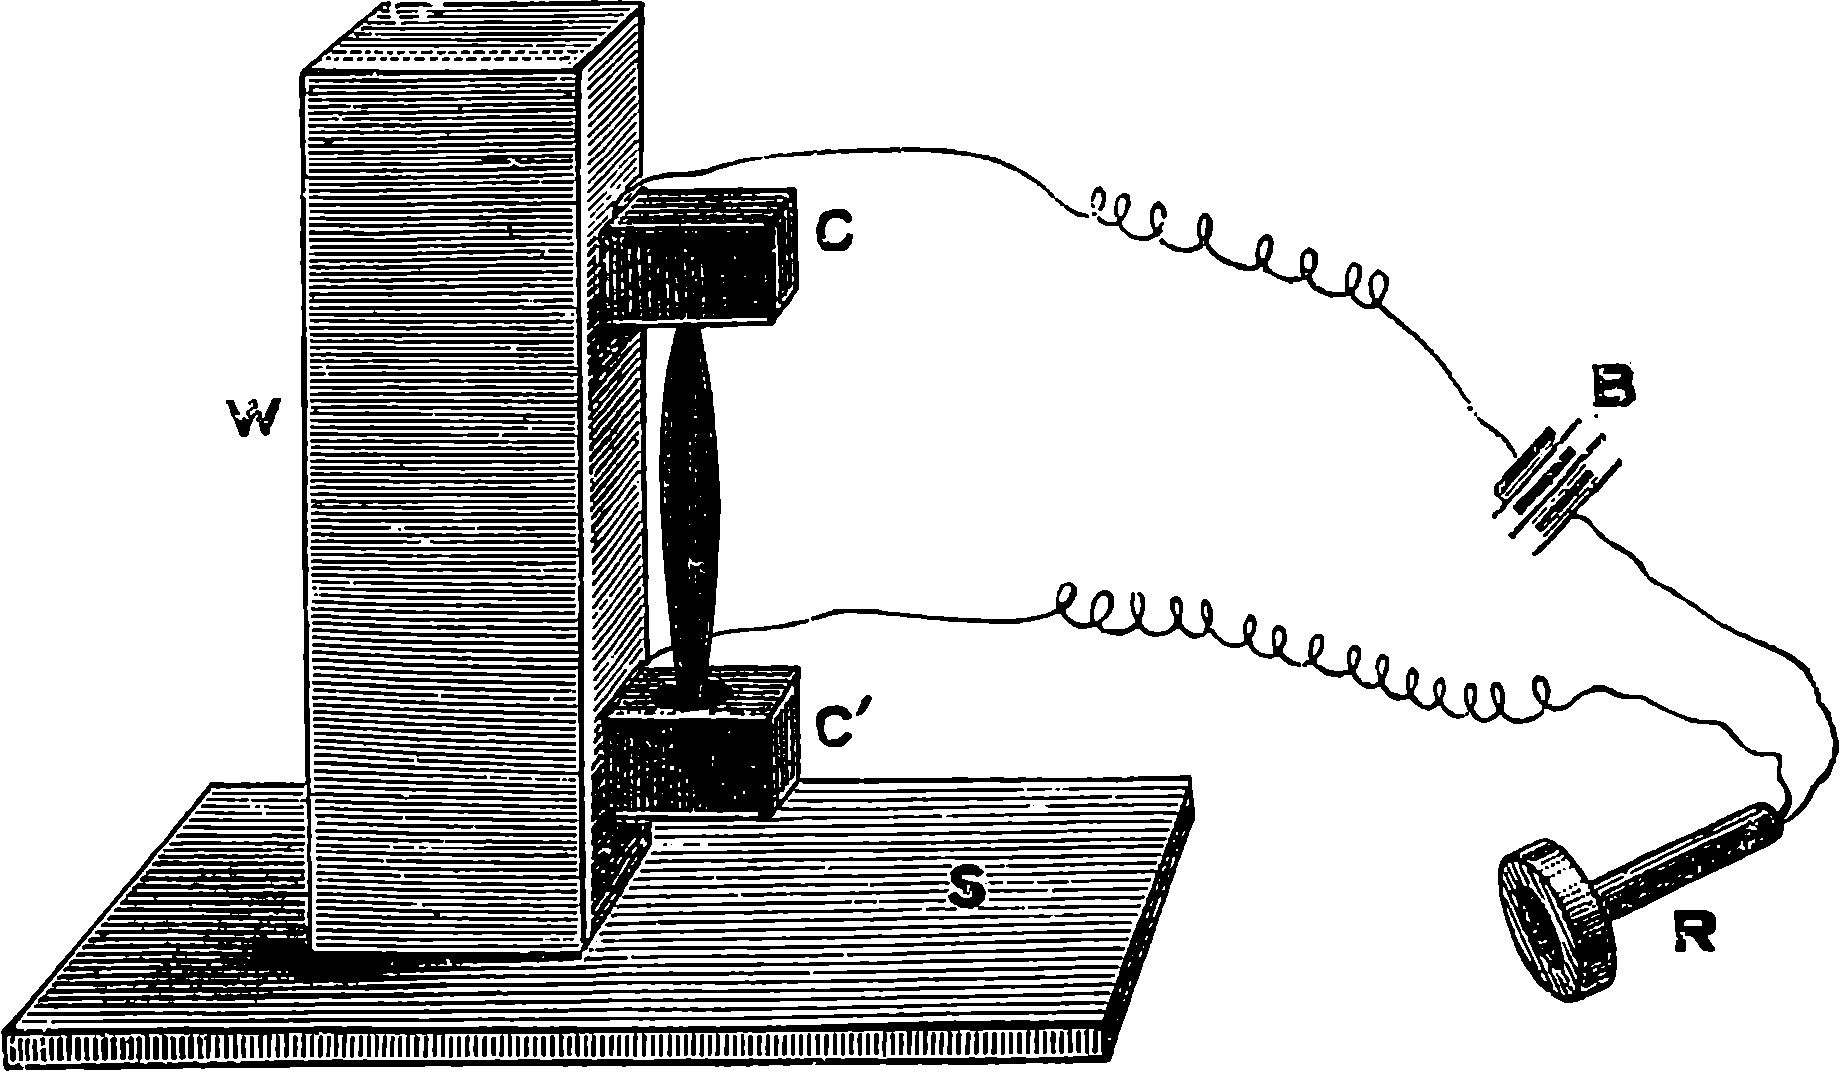
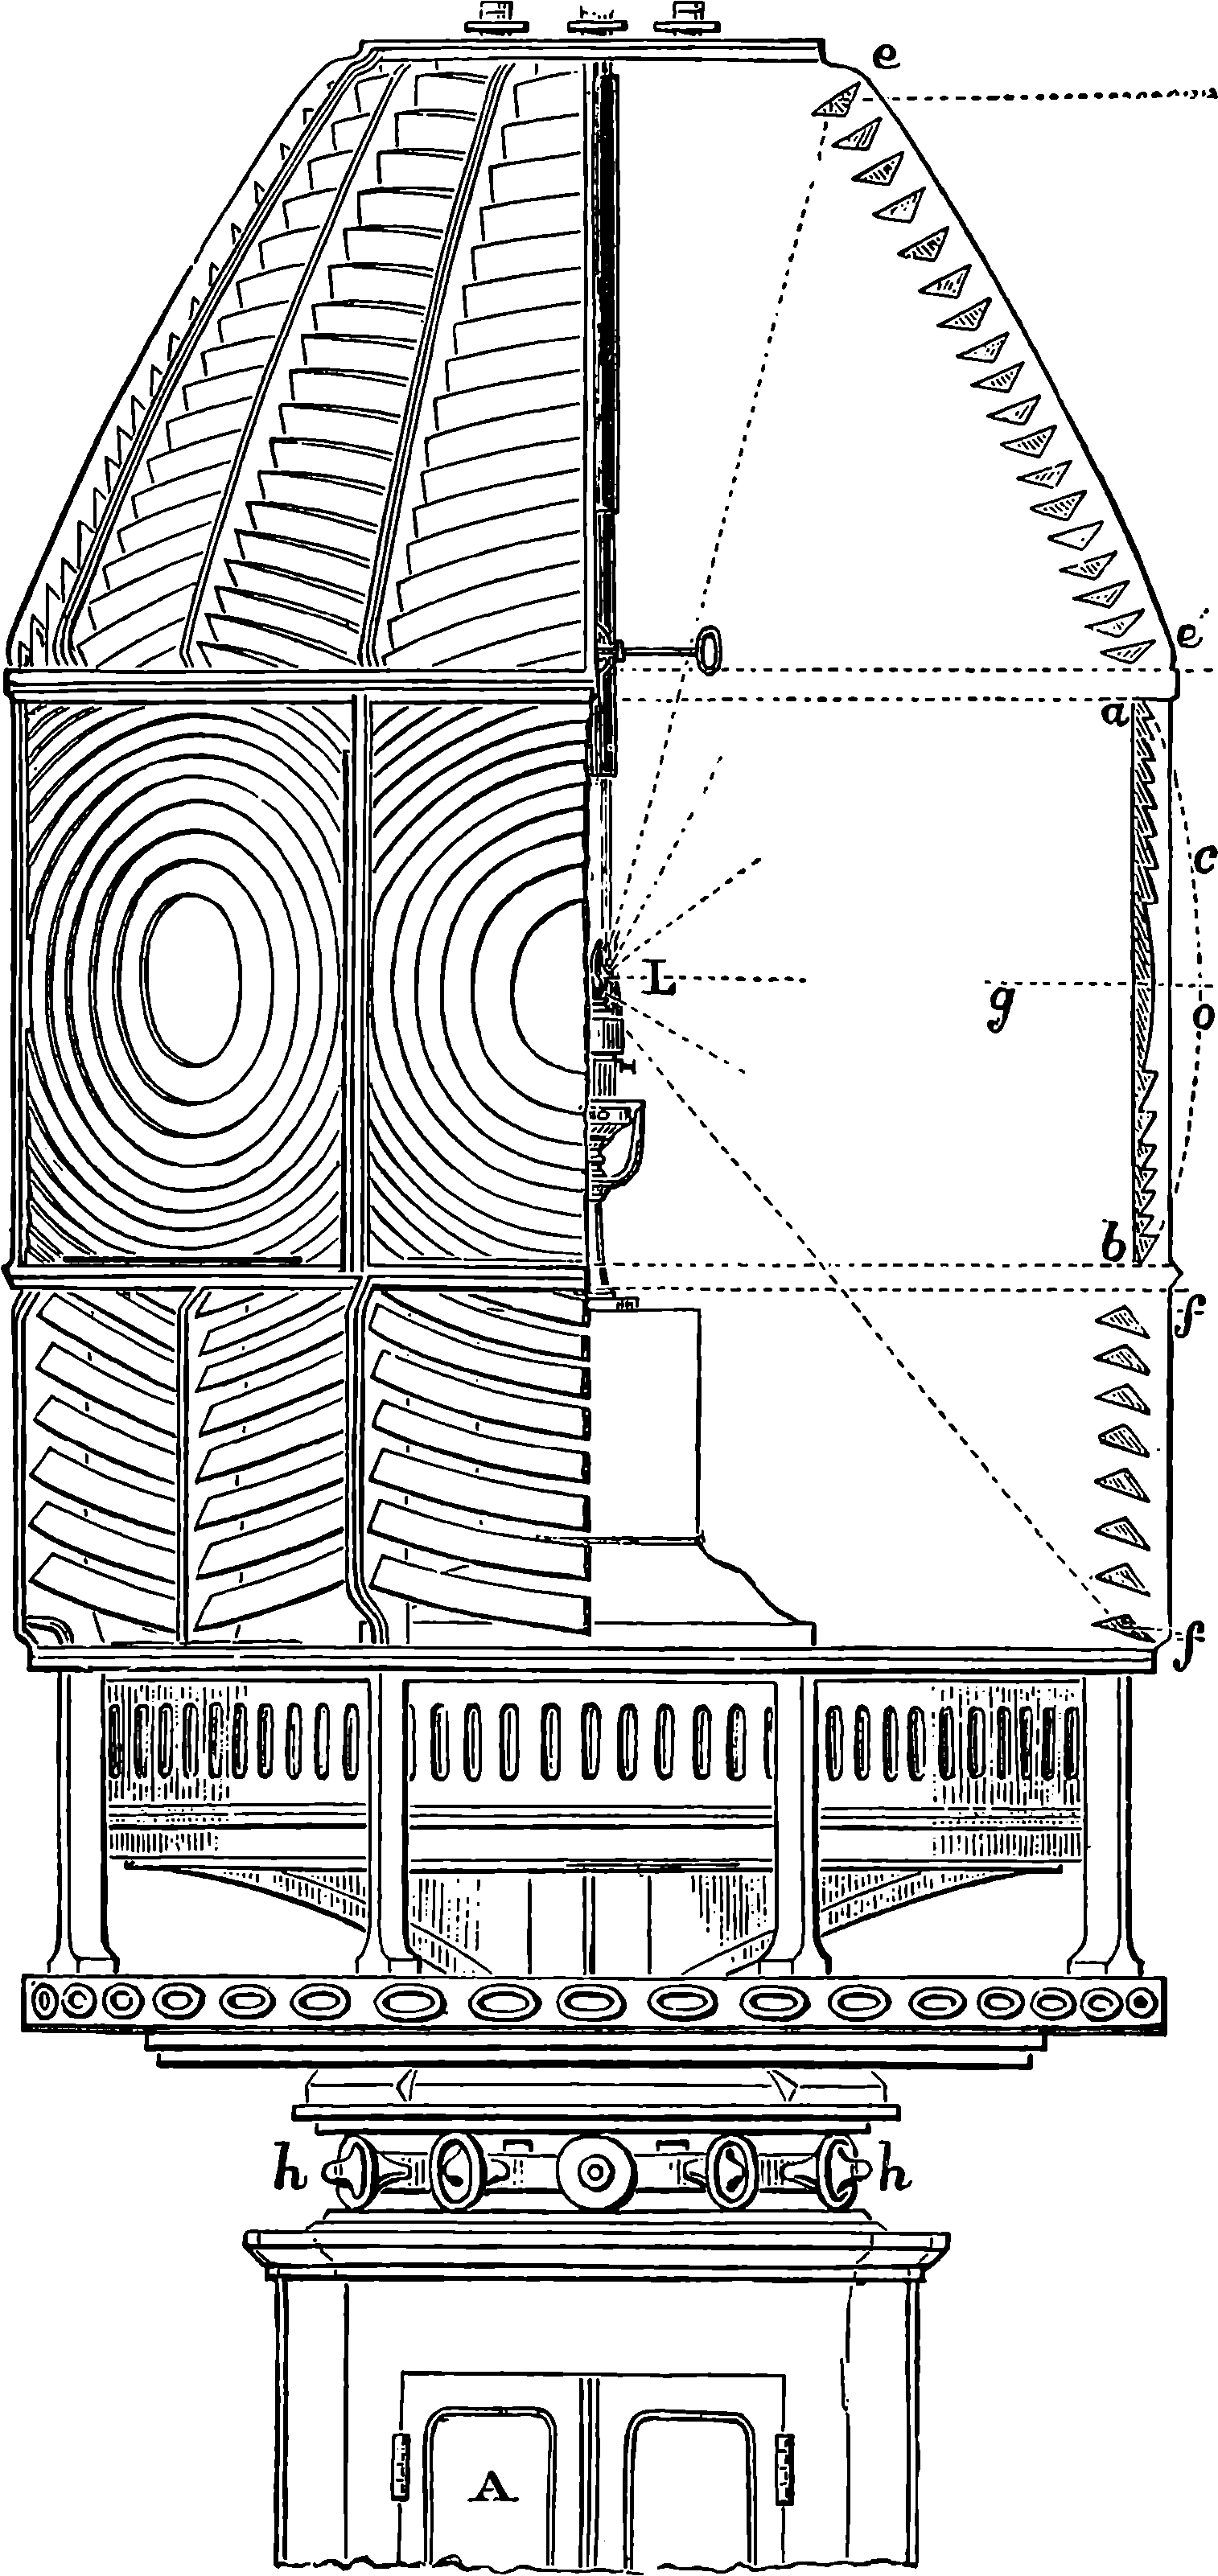
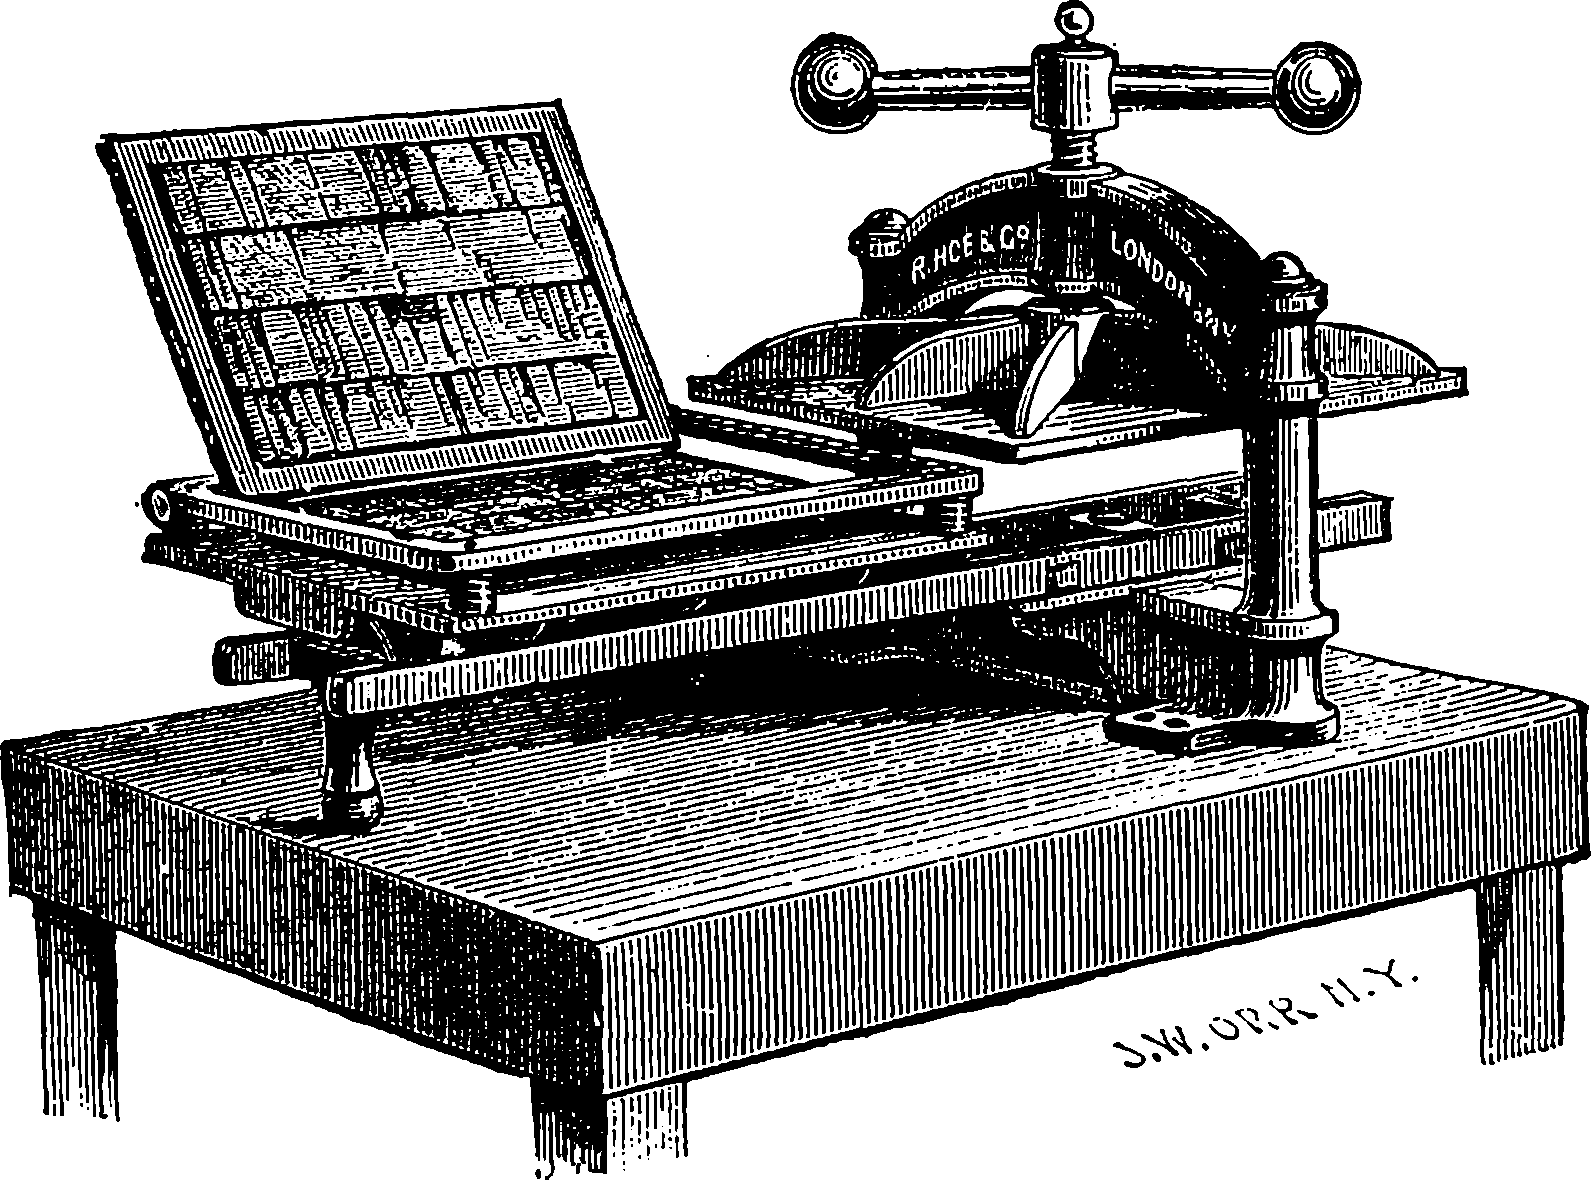
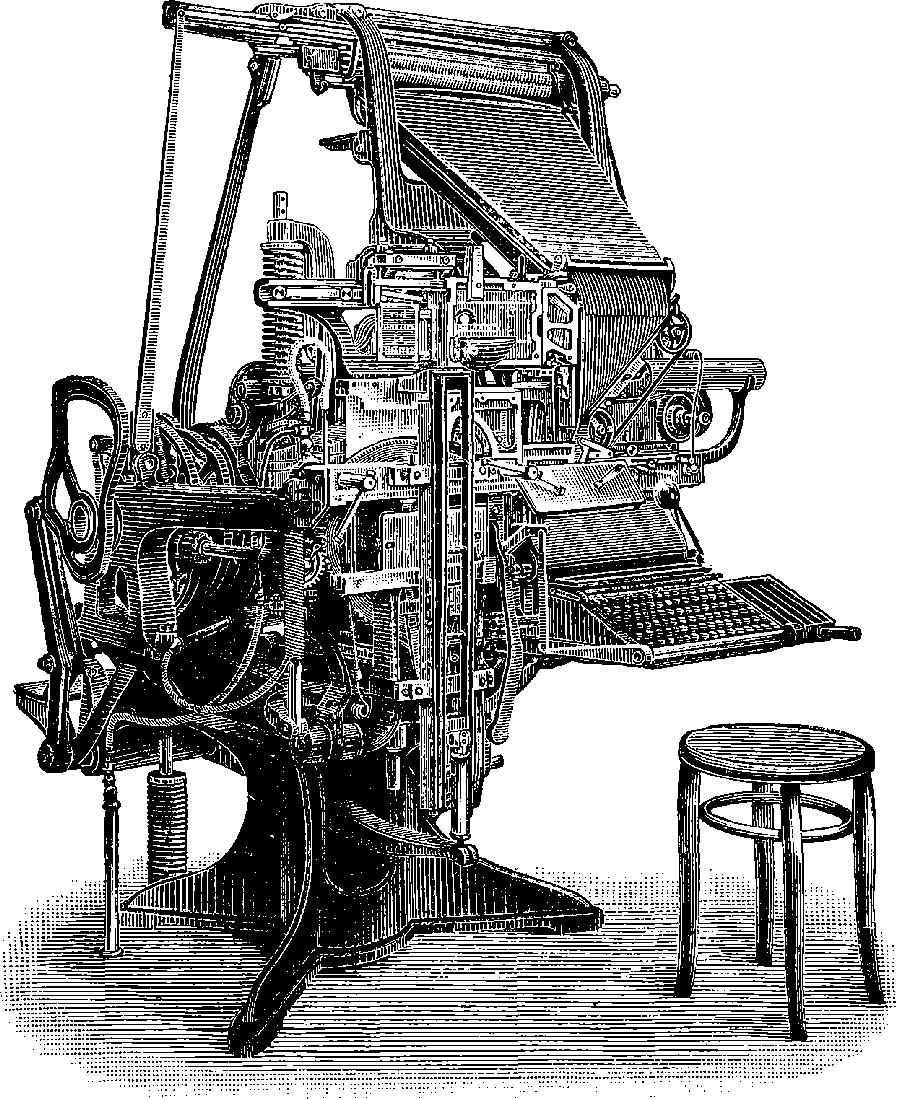
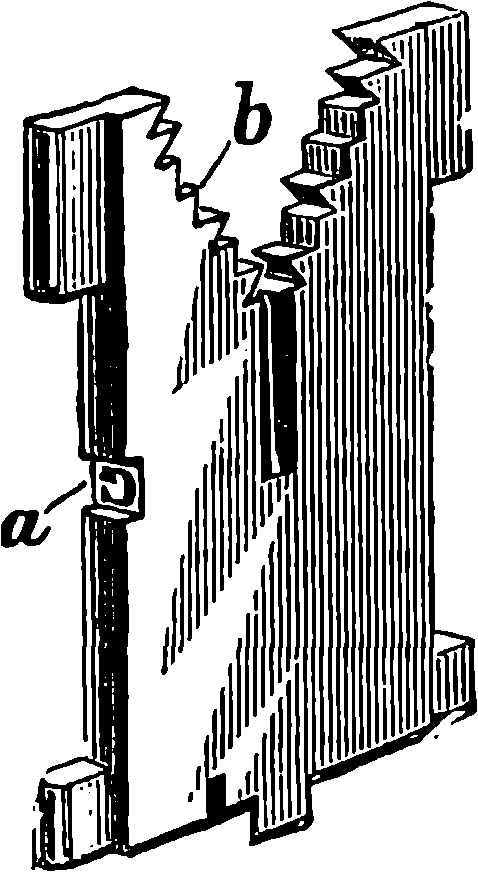
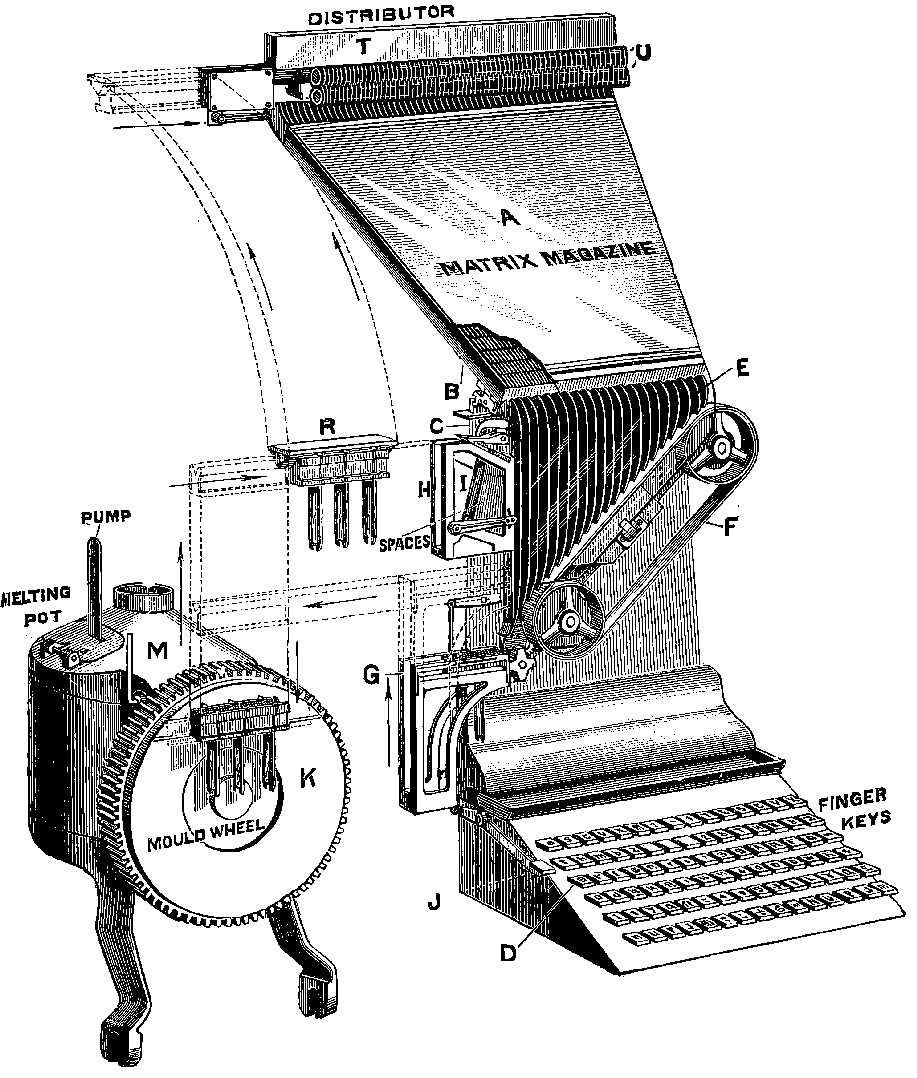
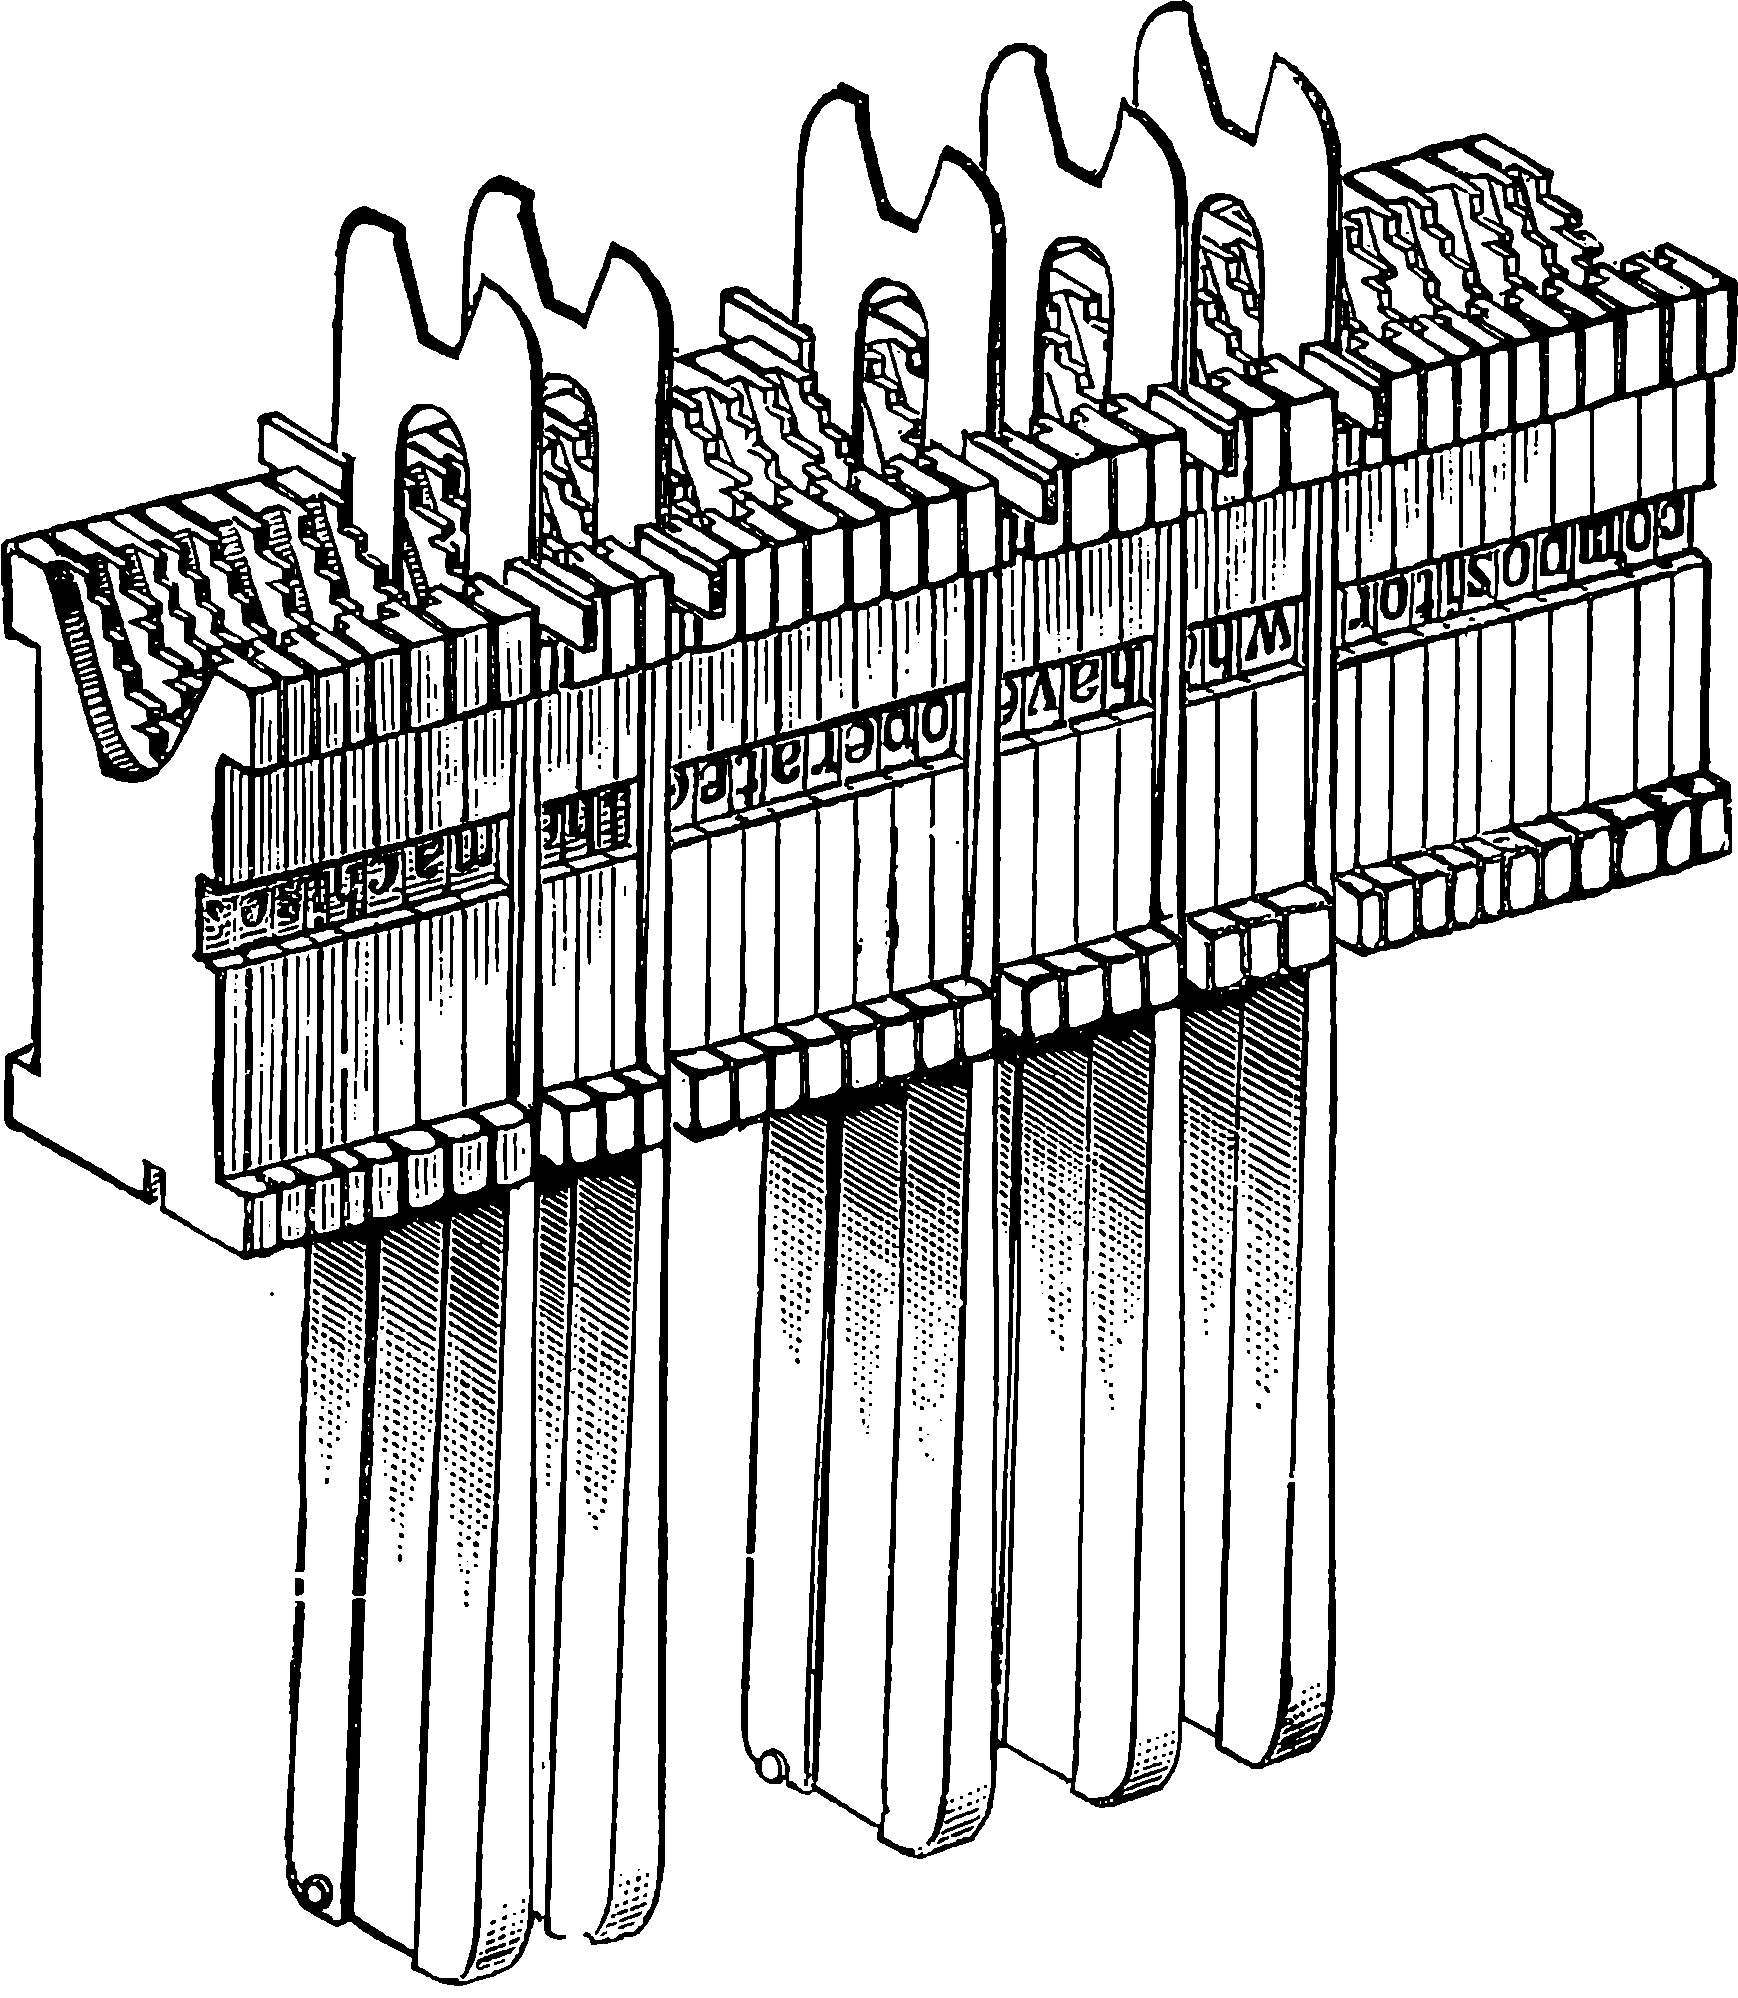
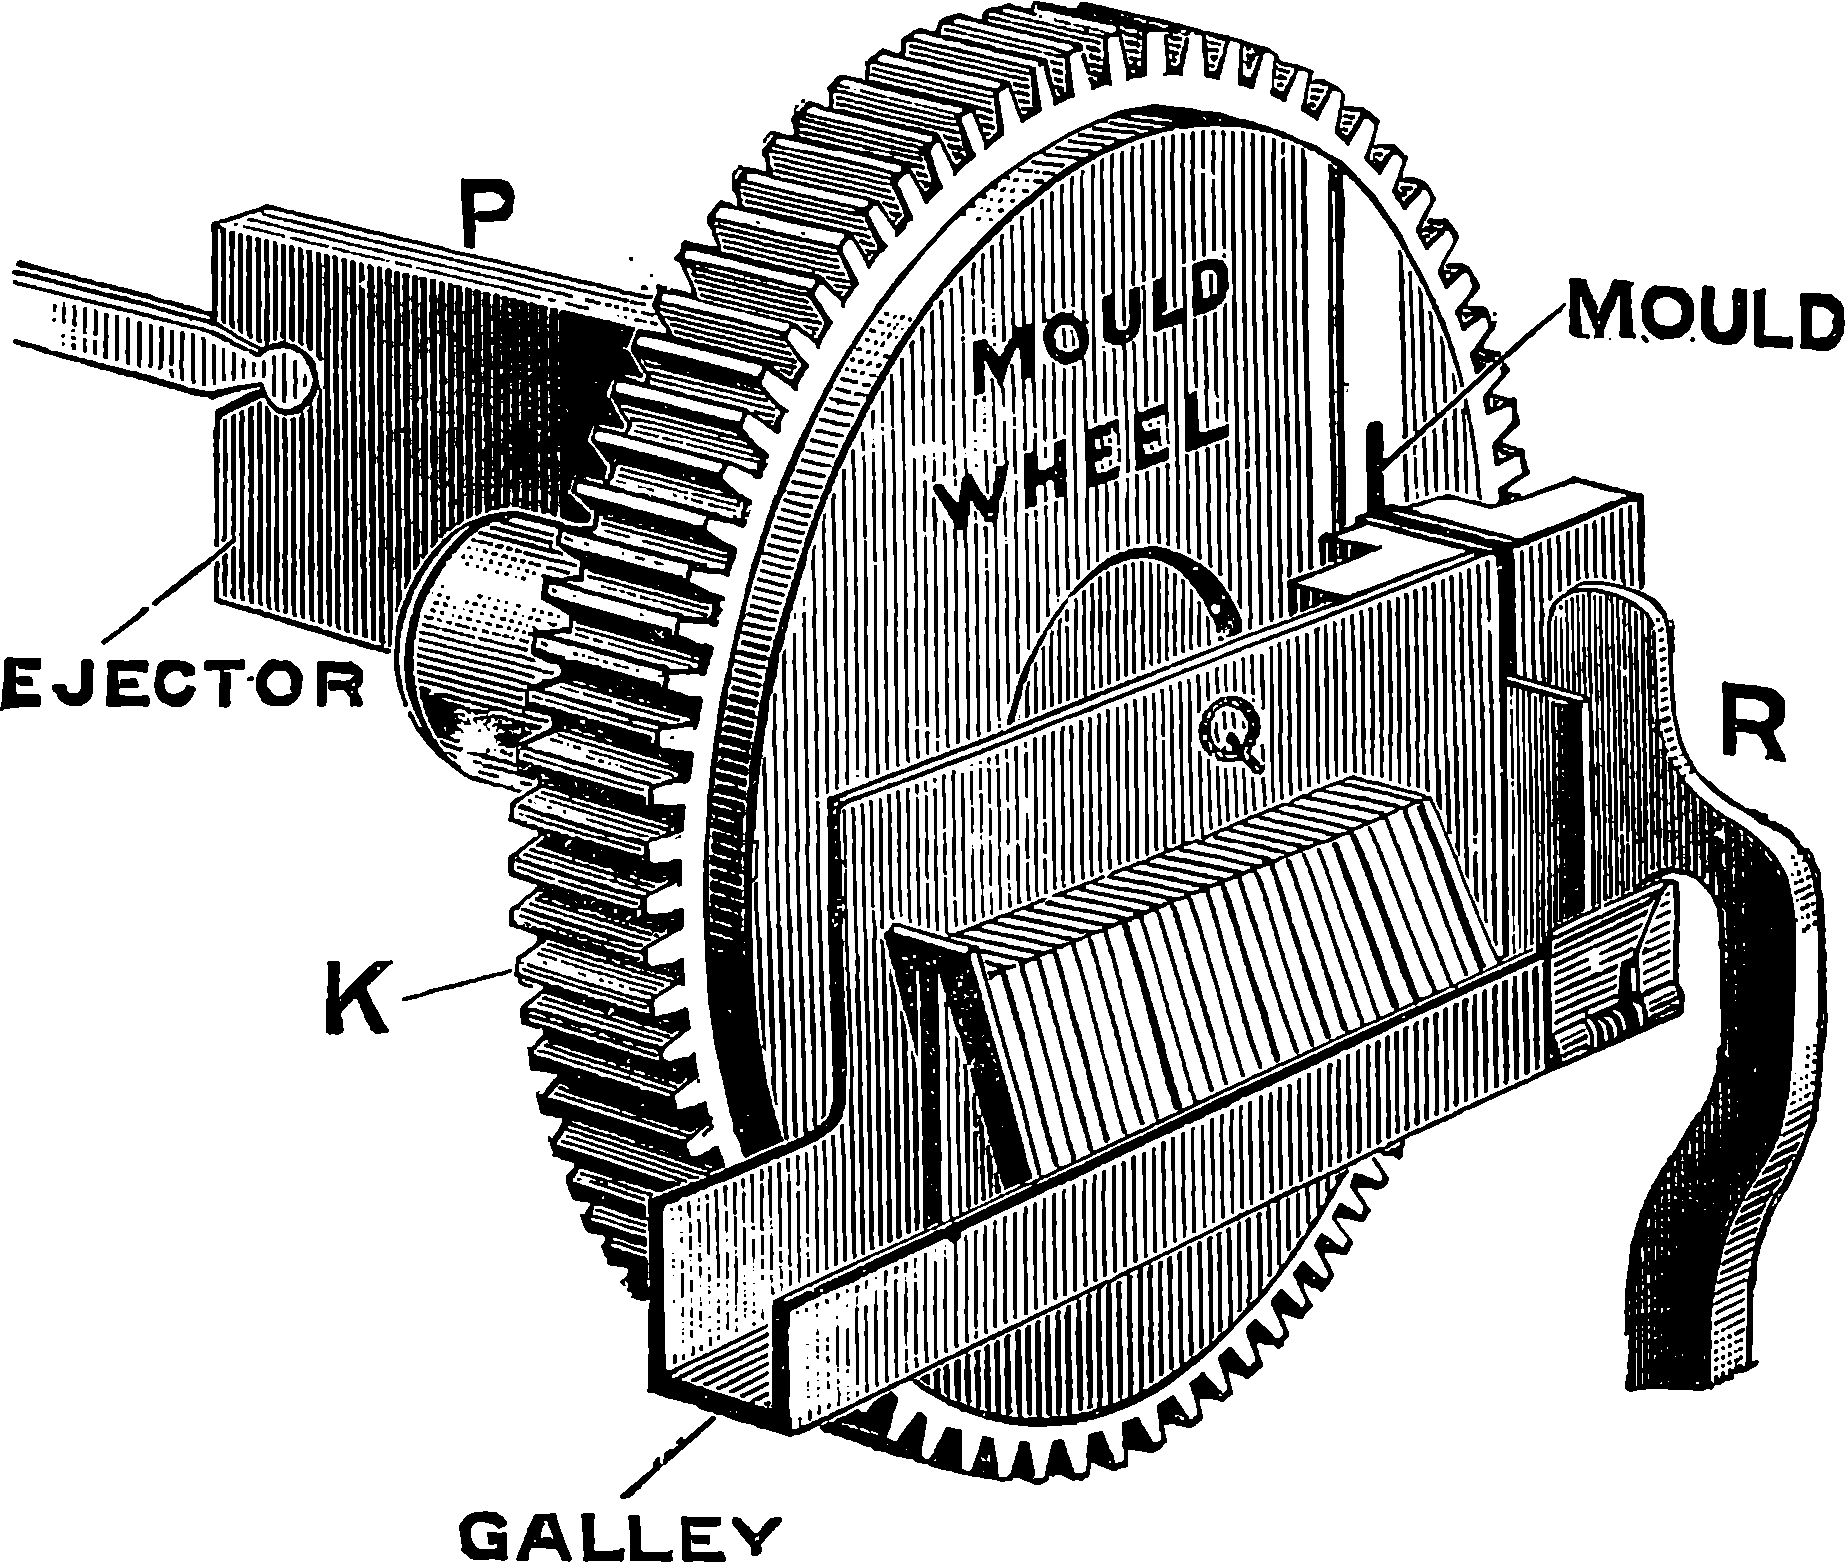
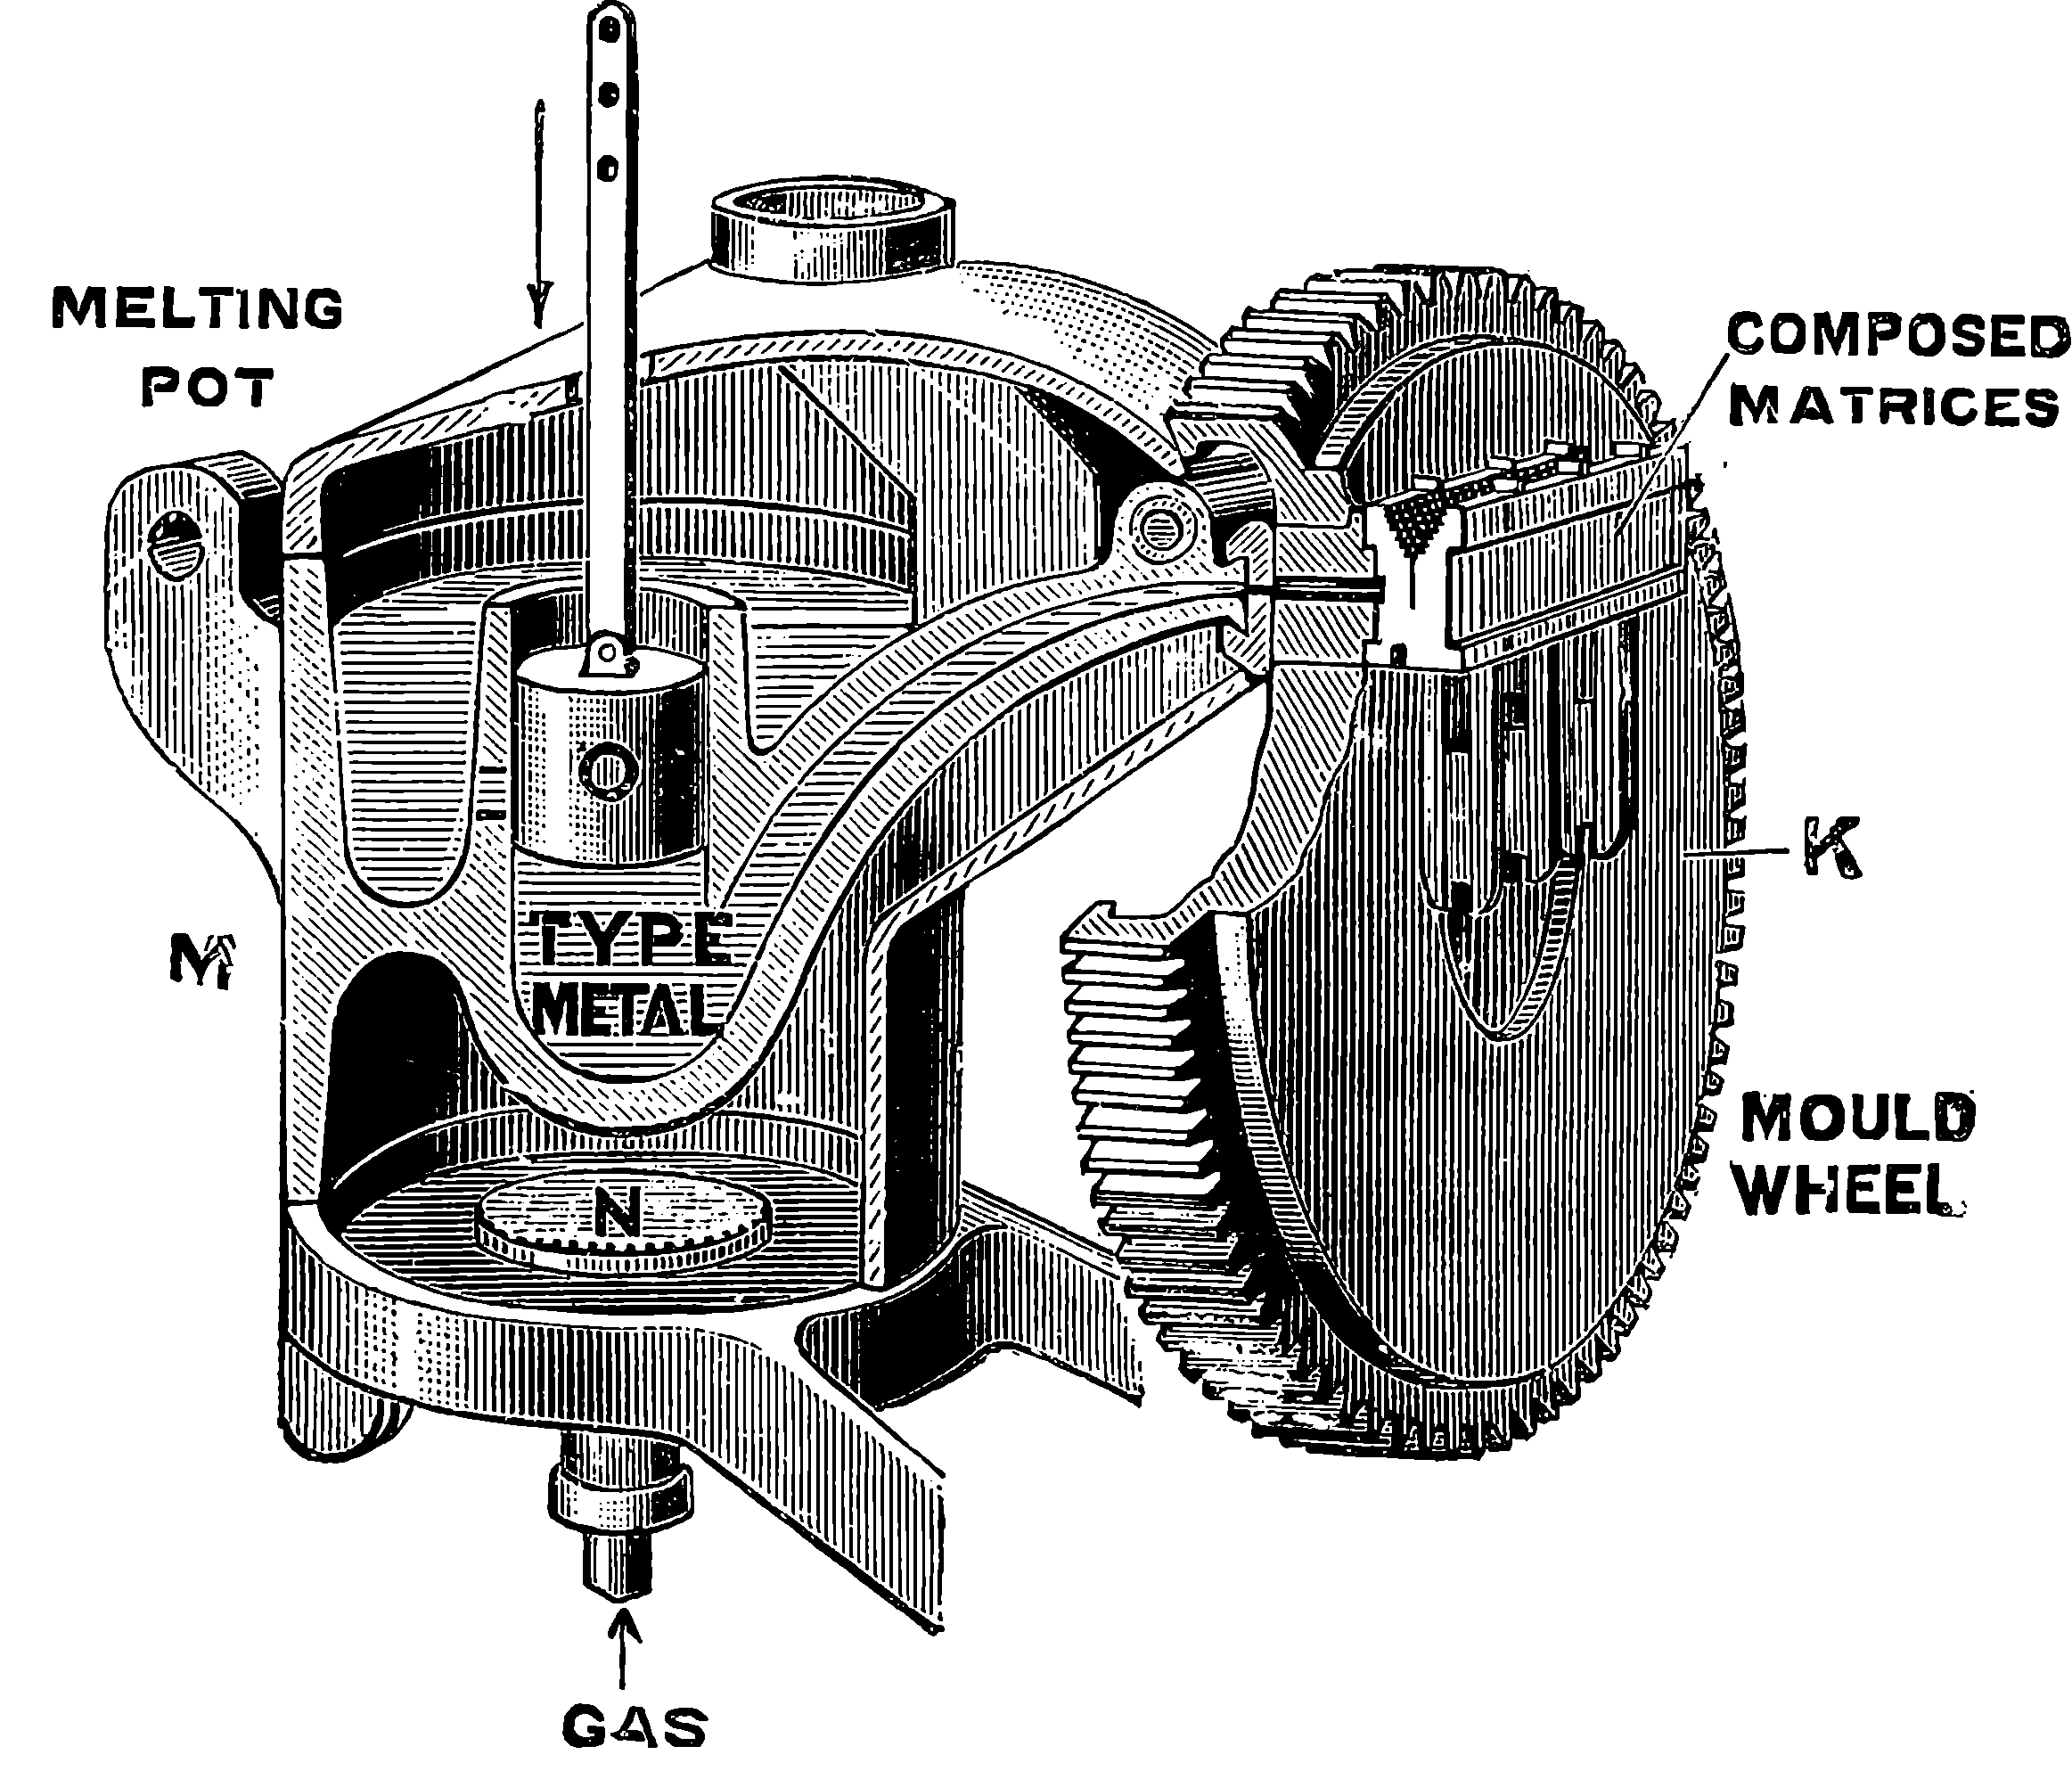
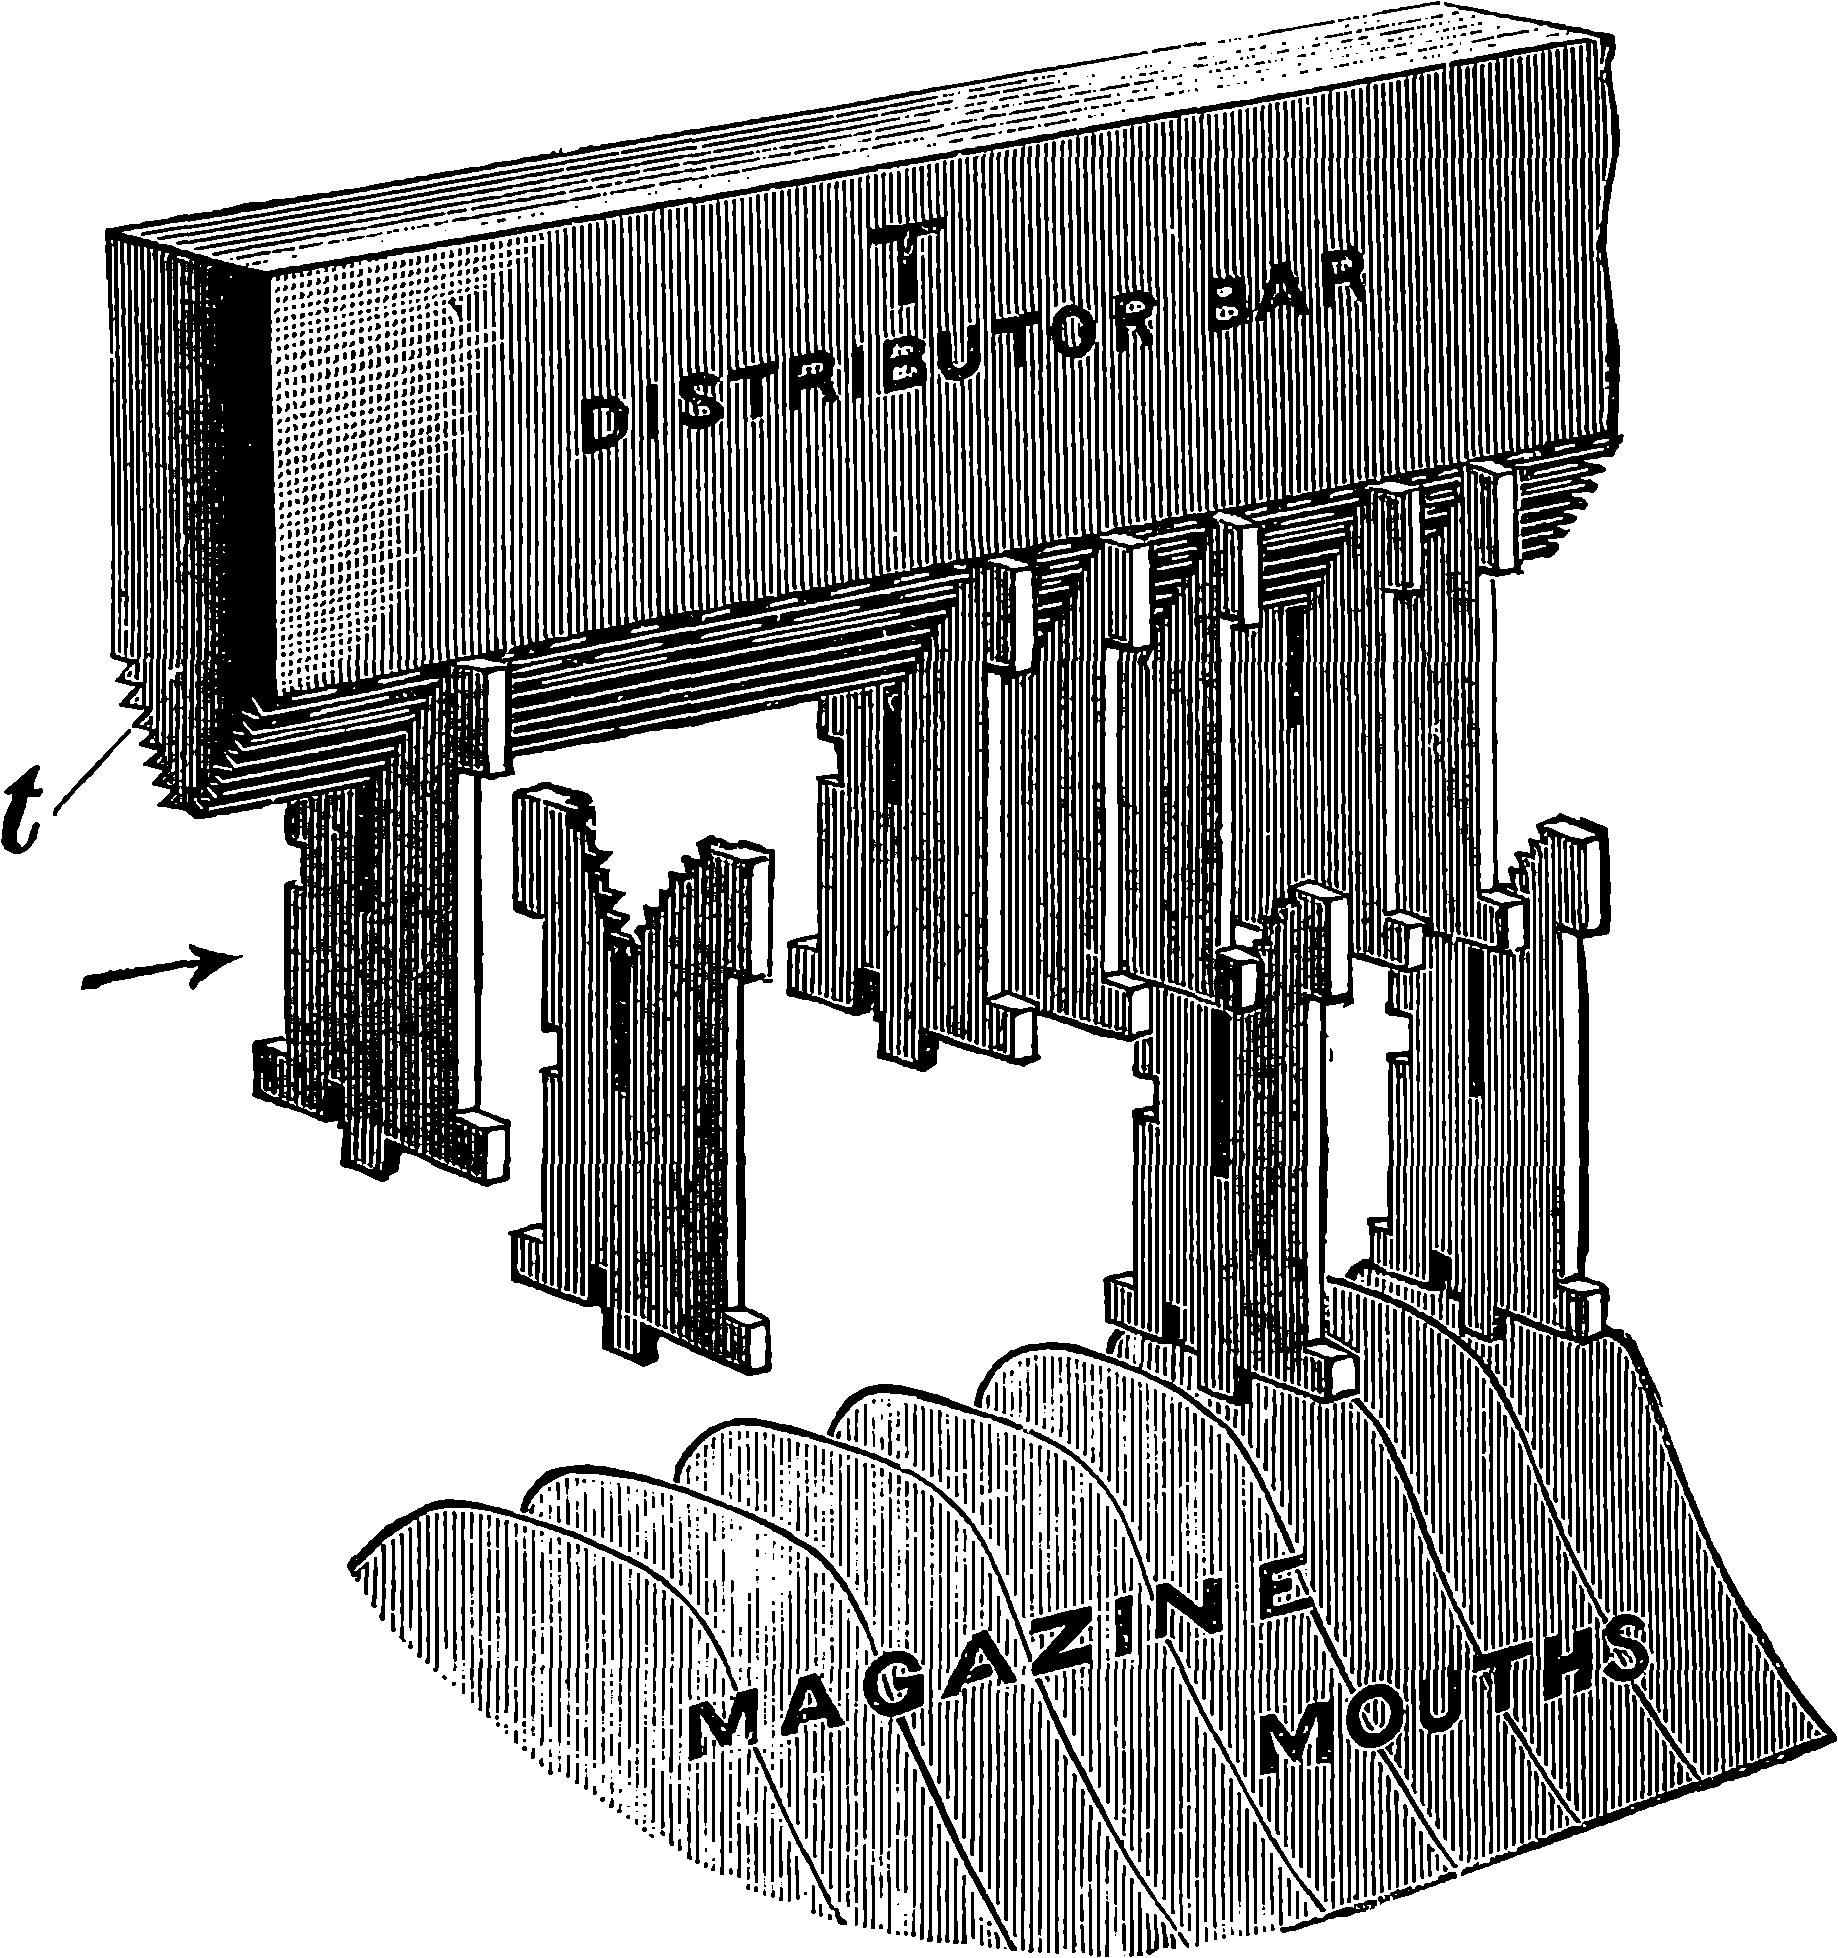
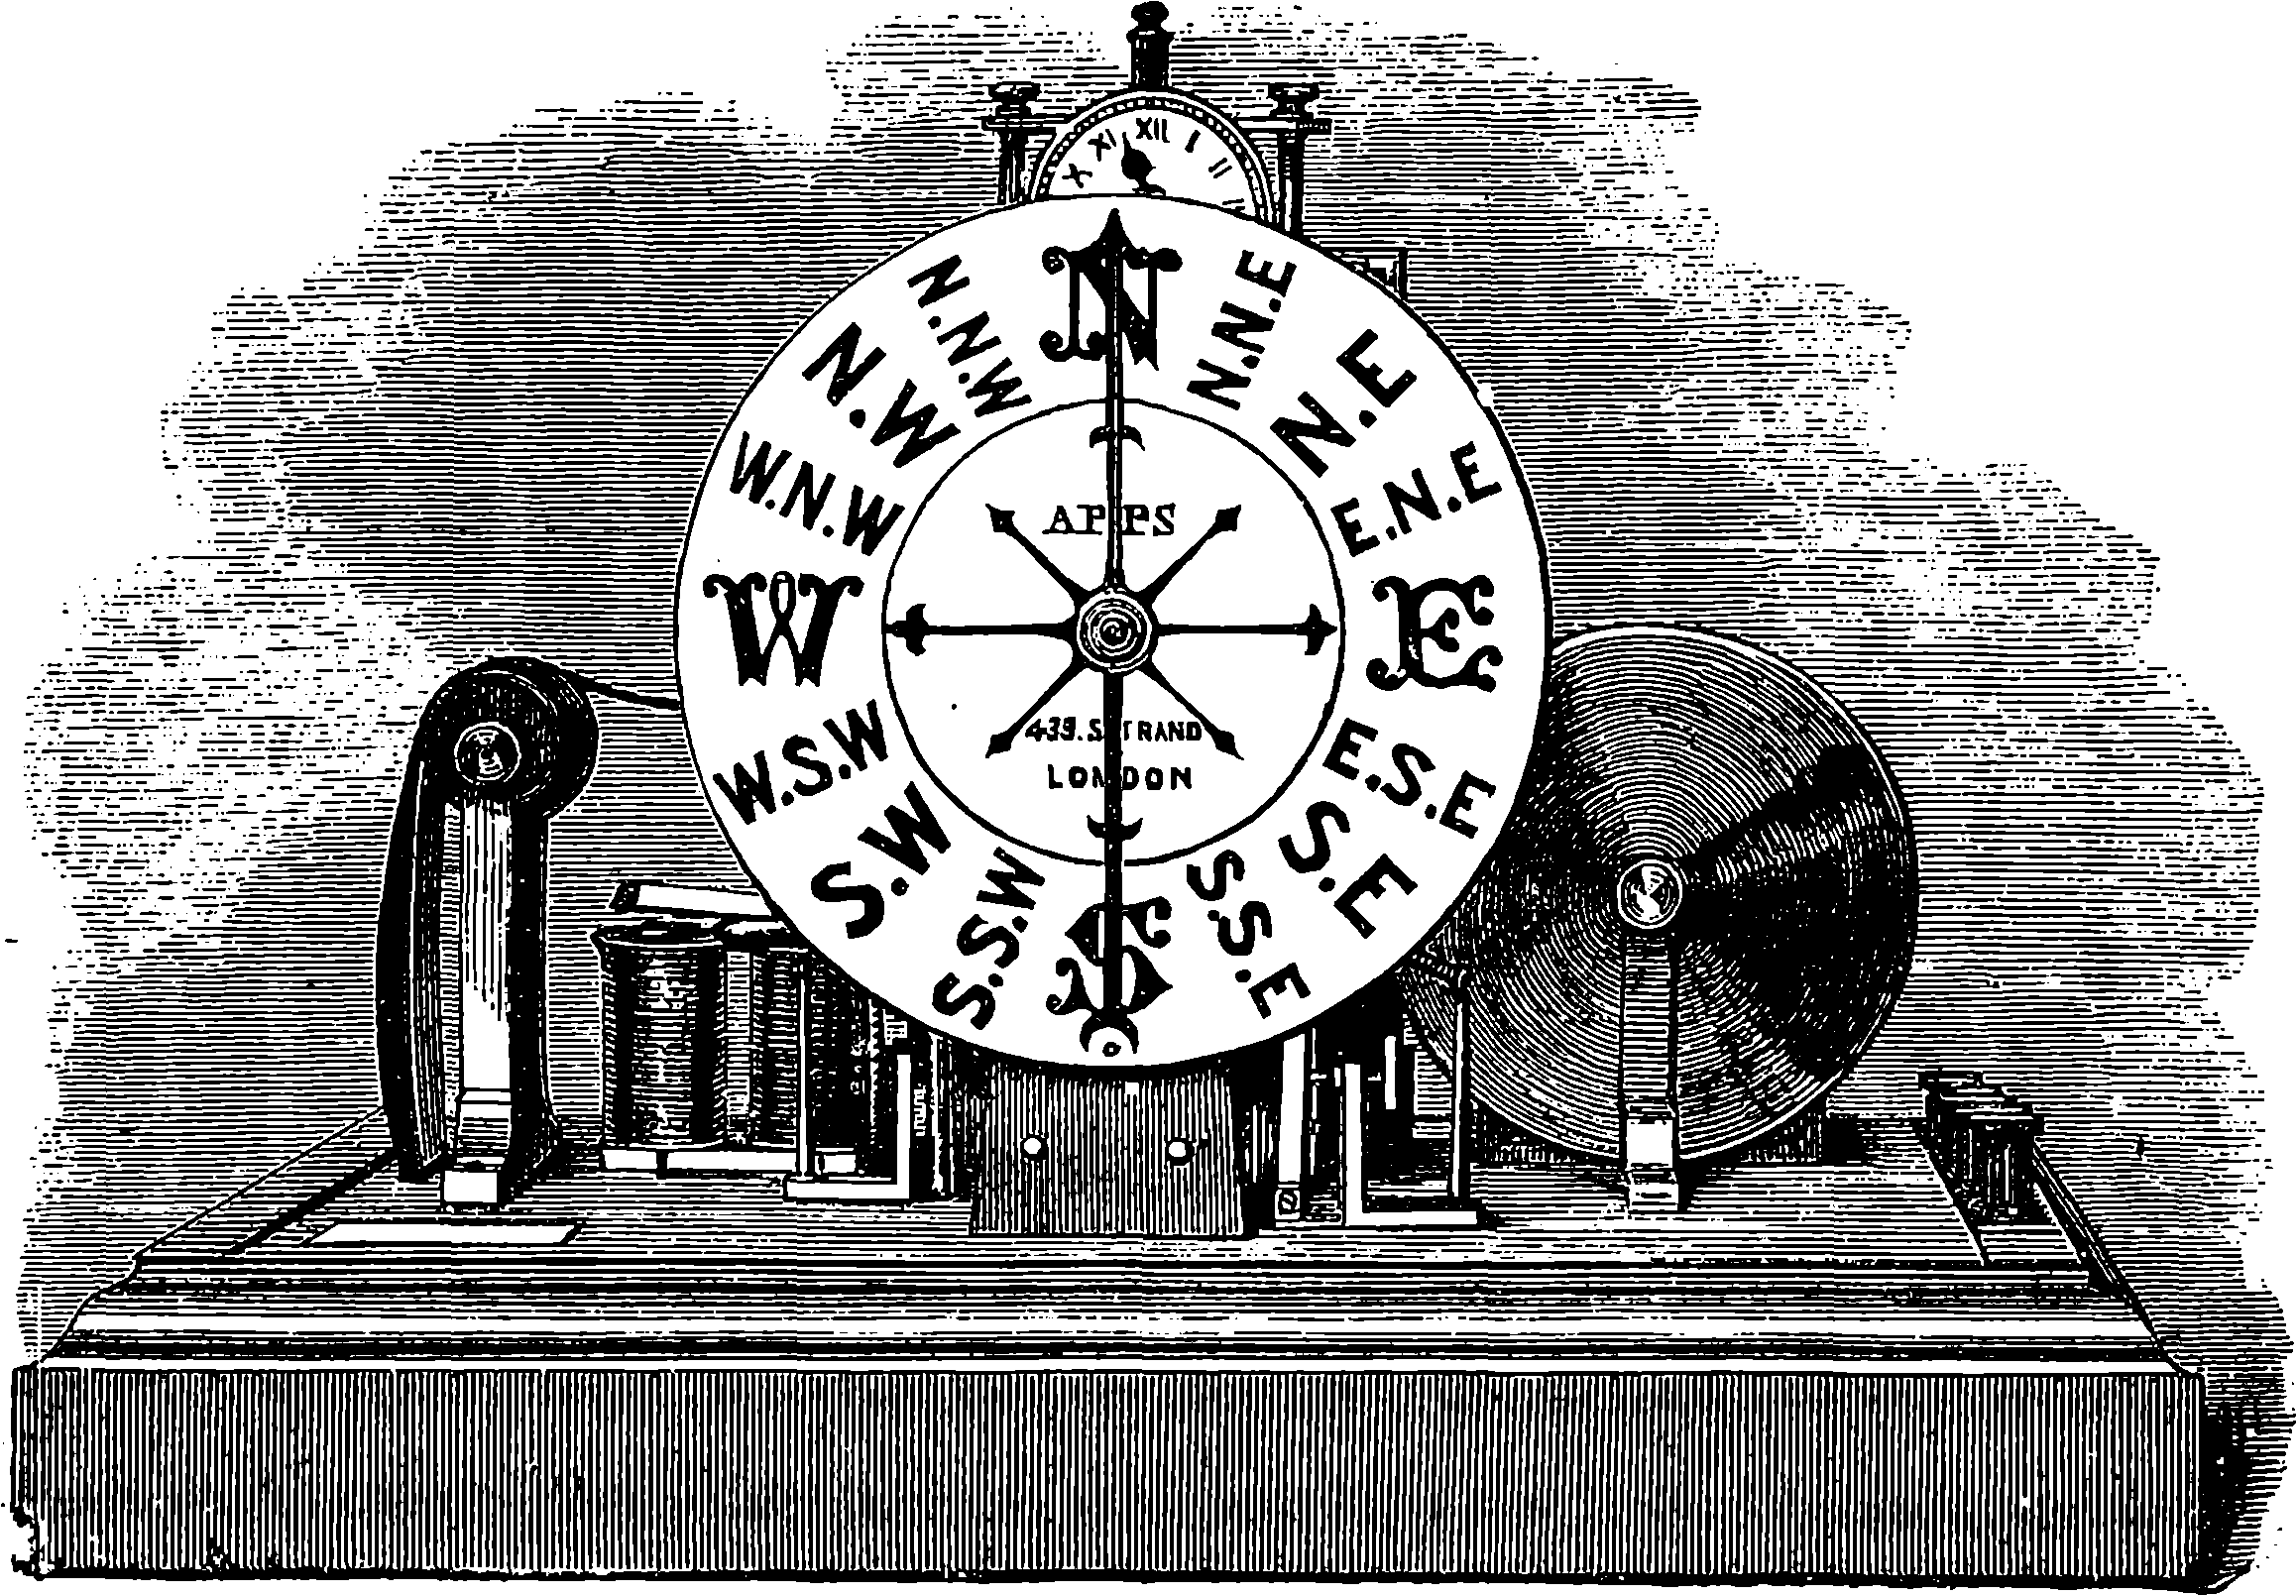
 , the establishment and interruption
of the current at the end of each second being marked with great
sharpness and precision.
 , and the
point where the deviation begins indicates the time at which the ball passed.
In order to read off this time, a straight-edge is applied to the cylinder
parallel to its axis; and by means of a scale sliding upon the straight-edge
the distances between the notches on the several spirals are compared
with those between the pendulum marks.