HEAD OF WEAVING AND DESIGNING DEPARTMENT, DUNDEE TECHNICAL COLLEGE AND
SCHOOL OF ART;
FORMERLY MANAGER, MESSRS. WALTON AND CO., LINEN MANUFACTURERS, BLEACHERS
AND FINISHERS, KNARESBOROUGH;
AUTHOR OF “THE FINISHING OF JUTE AND LINEN FABRICS”; “HEALDS AND REEDS
FOR WEAVING, SETTS AND PORTERS”; JOINT AUTHOR OF “TEXTILE DESIGN:
PURE AND APPLIED”; “JUTE AND LINEN WEAVING MECHANISM”;
“CALCULATIONS AND STRUCTURE OF FABRICS”; “JUTE AND JUTE
SPINNING,” ETC.
AND
P. KILGOUR
HEAD OF THE SPINNING DEPARTMENT, DUNDEE TECHNICAL COLLEGE AND SCHOOL
OF ART;
FORMERLY MANAGER, BELFAST ROPE WORKS; JOINT AUTHOR “JUTE AND JUTE
SPINNING,” ETC.
London Sir Isaac Pitman & Sons, Ltd., 1 Amen Corner, E.C.4 Bath, Melbourne and New York
Printed by Sir Isaac Pitman & Sons, Ltd., London, Bath, Melbourne and New York
PREFACE
The function of a small article in commercial undertakings
is often overshadowed by that of the larger
and usually more valuable article, and yet the use of
the former is often an absolute necessity for the safety
of the latter. This relative value is emphasized in the
use of cordage, because the successful prosecution of
many industries depends in no mean way upon the
utilization of this useful and common commodity.
Some of the various types of cordage are well known
to the general public, but the methods employed in
their manufacture, the machinery used, and the sources
of the fibres are not quite so well known. We trust
that these phases are discussed in as brief but as complete
a way as is possible in this little book, which we
hope will take its own place in the literature of our
Common Commodities of Commerce.
We take this opportunity of recording our warmest
thanks to Messrs. David Bridge & Co., Ltd., Castleton,
Manchester, for loan of blocks; to Messrs. The Edinburgh
Roperie and Sail Cloth Co., Ltd., Leith, for
assistance and for several photographs; and to Messrs.
Landauer & Co., London, for some of the statistics
regarding the fibres.
Records of civilization are incapable of furnishing the
era when the equivalent of strands or cords were first
used, singly or collectively, for the purpose of holding
two or more articles securely in position. But, although
it is impossible to fix a period, one might safely say
that the original material which served the purpose was
some kind of light twig or lanceolate leaf, and that its
appearance when in use as a binder strip differed little
if at all from its appearance in the natural process of
growth. Even at the present day some of these runners
are still used, notably with others the rattan canes for
binding bales of manila fibre and other purposes.
The wants of prehistoric man would be very few
indeed, but, although he was accustomed in many
climates to make use of very scanty clothing or covering,
and, in many cases, was practically without any
covering, it is obvious that it would be necessary to
provide himself with food—the first essential condition
to life. In his efforts to secure the necessary food-stuffs,
animate or inanimate, it is safe to conclude that
some type of ribbon-shaped vegetable material would
be necessary or desirable at an early stage, and probably
at the same time or a little later period sinews of
different kinds would be brought into use.
As years rolled on, further uses would undoubtedly
be found for various kinds of fibrous material, and more
improved methods would be applied in adapting the
vegetable matter and the like to the purposes intended,
as well as more care exercised in the selection of the
materials. Some of the characteristics which are
essential in practically all binders or tying strips
are length, strength, pliability and a tendency
to resist atmospheric influences and other natural
agents.
The gradual development of civilization, and the
gradually increasing demand for suitable substances to
be used as binders and for various other purposes would
naturally lead to improvements in the utilization of
fibrous and other suitable plants, and ultimately to
more or less scientific methods of treating these plants
with the object of removing the objectionable constituents
which are useless for cordage purposes, and of
retaining those parts which are considered to be most
suitable for the purpose in view.
A complete description of the evolution of modern
cord and cordage is practically impossible, for the
simple reason that there is no full record of the efforts
of many of the earlier pioneers in the various stages,
and it is quite possible that many early and praiseworthy
improvements have been forgotten or overshadowed,
or perhaps absorbed, by the more modern
and more elaborate methods which are now indispensable
for the successful prosecution of this important branch
of the textile industry.
The separation of fibrous material from various kinds
of plants is by no means of modern origin, for the great
antiquity of yarns which have been spun from vegetable
and animal fibres is universally acknowledged. Reference
to the process of preparing flax for the purpose of
spinning appears in Exodus ix, verse 31, while the first
Biblical reference to thread—one of the technical names
for a continuous length of prepared fibrous material—is
in Genesis xiv, verse 23: “That I will not take
from a thread even to a shoe-latchet.” Again, another
early reference in Chapter xxxviii refers to a scarlet
thread, an indication or suggestion that the art of dyeing
was also known at this early period in the early
Biblical history.
Herodotus records garments made from hemp by the
Thracians, and to the present day hemp is largely cultivated
in the vicinity of the lands occupied by the
descendants of this ancient race.
Moschion, whose writings appeared before the Christian
era, states that the “great ships of Syracuse which
were built by command of Hiero II were supplied with
hemp and ropes from the Rhone districts. Hemp was
brought from Colchis to the ports of the Aegean Sea
by the merchants who were connected commercially
with the north and east coasts of the Euxine through
their Milesian colonies.”
Pliny also records the use of hemp for ships, and
states that it was in common use among the Romans
in the first century for ropes and sails, as well as for
other purposes.
The more or less uncertain knowledge of practically
all the earlier attempts at the solution of fibre extraction
renders it impossible for us to bridge the gap
between the time when crude primitive methods were
practised and that which ushered in the more perfect
methods described by Pliny in the first century—methods
which, in certain cases, have varied little since
this early period, and which are practised with a high
degree of success. We may, therefore, leave this interesting
period to the researches of students in history,
and enter upon the description and illustration of the
various plants from which fibre is extracted, and the
actual processes which such fibre has to undergo before
it is ready for the market in one or other of the
well-known types of cordage.
CHAPTER II DEFINITION OF CORDAGE AND SOURCES OF FIBRES
The definition of cordage usually takes the form of “a
quantity of cords or ropes as the rigging of a ship, etc.,”
but in commerce the word has a more elastic meaning,
and, in general, may be said to include all kinds of
continuous strands or the like which are not intended
to be woven into cloth or to be knitted into hosiery.
Differentiation occurs, however, for one often finds the
phrase “Ropes, Cords and Twines” as referring to
special types of cordage, while further subdivision occurs
when one includes the many types of finer material
such as lines, sewing thread, and the like. And when
one considers that the various articles which are included
in the generic term cordage have a range from ropes
of 9 or 10 in. in diameter to fine threads of not more
than perhaps 1/60th of an inch, and for which a very
large number of different kinds of fibres are used, some
idea of the immense variety can possibly be formed.
From whatever source a vegetable cordage fibre is
derived, it is necessary to eliminate more or less of the
substances which are closely connected with it in the
plant, in order that the comparatively pure fibre may
be spun into thread form with the maximum of strength
and production, and the minimum of difficulty and
waste. In this respect it is quite likely that an animal
fibre such as wool would be more easily separated than
any other known fibre. Wool, however, is rarely used
for cordage purposes, although hair, which approximates
to wool, is used for certain types of cord. There are
certainly many types of wool ropes used for decorative
purposes, but, in general, this most valuable substance
is, for obvious reasons, unsuitable for the usual kind
of cordage, and hence wool will not be discussed in this
work.
The fibres from the leaves of certain tropical plants
may be separated with a little more difficulty than that
which is experienced in the operation of shearing a
sheep, but these fibres are hidden, and even when found
originally, great difficulty would be experienced before
a continuous thread could be made from them. It is
quite probable that a natural process of disintegration
would disclose these vegetable fibres to primitive man,
and lead to their ultimate utilization for various purposes.
Or perhaps the gradual wear and tear of the
leaves used, either loosely or bound in some crude form,
as floor-covering would result in the discovery of the
fibrous layers. It is the remarkable advance in mechanical
science which has made the production of a continuous
thread from such fibres a possibility for industrial
purposes.
Long before continuous spinning was invented, however,
it would be desirable to extract the valuable fibrous
material from its bed of vegetable matter because the
latter is, in general, quite unfit for the purposes which
the fibrous material has to perform. This remark
applies not only to the fibres which are extracted from
leaves, but also to those valuable fibres which are
embedded in the bast layers of the stems of certain
plants.
We might now with advantage illustrate by means
of photographic reproductions of plants, and photomicrographs
of sections, the three sources from which
vegetable fibres are obtained to be utilized in the manufacture—or
spinning as it is technically called—of the
world’s supply of cordage.
By permission of Messrs David Bridge & Co., Ltd. Fig. 1 TWO-YEAR-OLD SISAL PLANT
A typical example of a leaf plant from which one
type of textile or cordage fibre is extracted is illustrated
in Fig. 1. This particular example is designated as a
“Two-year-old Sisal Plant.” It is 49 in. high, and was
grown in the Voi district, British East Africa. Sisal is
the commercial name of the fibre obtained from such
plants, while the botanical name of the plant is Agave
Rigida, variety Sisalana; it is sometimes, though
erroneously, termed the Americana.
Fig. 2 AGAVE AMERICANA
A recently suggested nomenclature of the Agave and
other plants, from which sisal and similar fibres are
extracted, is due to Professor Lyster Dewey of the
United States Department of Agriculture—
(1) Agave Fourcroydis of Yucatan; this plant yields
90 per cent. of the sisal fibres exported from all countries.
The leaves bear marginal spines as illustrated in the
Agave Americana shown at A, Fig. 2: the plant was
formerly known as Agave Rigida, variety Elongata.
(2) Agave Sisalana grown for use by the natives of
Central America and South Mexico, but not much
exported.
(3) Agave Cantala. This is the “Maguey” plant of
the Philippine Islands, and is grown in limited quantities
in Java and India.
Fig. 3 TRANSVERSE SECTION OF A LEAF OF AGAVE AMERICANA
When a thin slice or fine transverse section of one of
the leaves of such a plant is mounted, and its appearance
magnified by photomicrography, the structure of
the leaf is shown to be similar to that illustrated in
Fig. 3. The upper and the lower outer surfaces or
cuticle A resemble greatly the whipped edges of blankets.
These surfaces, and all the pulp-like matter lettered B,
must be removed, either by manual or mechanical
means, in order to separate or extract the groups of
fibre some of which are denoted by the letter C. A still
further enlargement of a few of these groups of fibrous
material appears in Fig. 4.
Fig. 4 PHOTOMICROGRAPH OF A SECTION OF FIBRES OF AGAVE AMERICANA
A photomicrograph of two fibres of a type of Agave
grown in Mexico is shown in Fig. 5; it is interesting
because it depicts the formation of crystals of Oxalate
of Potash. The presence of such crystals makes the
fibre unsuitable for cordage purposes, but it may be
used in the manufacture of coarse brushes.
Fig. 5 PHOTOMICROGRAPH OF FIBRES OF AGAVE GROWN IN MEXICO, SHOWING OXALATE OF POTASH CRYSTALS
The second source from which fibre is extracted is
that from the stems of plants such as flax, hemp, jute
and the like. A photographical reproduction of a group
of hemp plants grown by the Authors appears in Fig. 6.
A female plant is illustrated on the right, while the
remaining two which are taller are male plants.
Fig. 6 GROUP OF HEMP PLANTSFig. 7 CROSS-SECTION OF PLANT
A thin cross-section cut from the stem of such a plant
exhibits the characteristics in Fig. 7, in which A is the
cuticle or outer bark, B is the woody part, and C the
pith. The fibrous layer is between the two dark circles
D, and a few groups of fibres in this layer are indicated
by the letter E. Here, again, a considerable amount of
extraneous matter must be separated from the bast
layer, and when separated, the latter appears in the
form of long ribbons. The cuticle and bast layer were
originally stripped from the plants; the former were
then placed in the mouth so that the saliva could aid
in the separation of the fibres from the bark, and permit
of a finer reduction of the fibrous layer to produce finer
threads. And although at the present time this method
is practised for thread making in many primitive communities,
it need hardly be said that much more efficient
methods have long been practised for commercial
purposes, such methods being known by the technical
terms “retting,” “breaking,” and “scutching.”
Fig. 8 LONGITUDINAL VIEW OF COTTON FIBRESFig. 9 CROSS-SECTIONAL VIEW OF COTTON FIBRES
The third source of vegetable fibres is the cotton plant
Gossypium, the white fluffy fibres being obtained from the
pods or bolls. The operation of cotton picking which is
often referred to consists of removing this white fluffy
mass from the pods in which also the seeds are located.
Cotton fibre is unlike the two previous classes of fibre
because its method of growth is different. The other
textile fibres are composed of bundles of plant cells,
whereas the fibres of cotton are individual cells; they
form as it were individual hairs on the seed, and in drying
flatten and also assume a twisted and crinkled condition
as exemplified in Fig. 8, which illustrates the
longitudinal characteristics of several fibres. Fig. 9
shows the sectional enlargements of a few fibres. This
structure of the cotton fibre is a very valuable property,
since it not only assists in the binding of the fibres into
a thread, but also gives a resiliency and spring to ropes
manufactured from it which is most useful in driving;
this property makes cotton almost indispensable for the
construction of the smaller sizes of ropes for driving
purposes.
CHAPTER III CLASSIFICATION OF FIBRES
Cordage fibres which are used at the present time are
naturally of greater variety than those which were
utilized for similar purposes in the early periods of
history, for records of those used in such early periods
appear to indicate only hemp and flax. As already
stated, wool would not be used to any great extent,
but, after methods had been evolved for spinning a
continuous thread from fibres such as hemp and flax,
it is highly probable that the cotton fibre would also
be used in the making of cords and ropes.
Authentic records point to the fact that the cultivation
of flax plants for fibre was practised in Egypt from
5,000 to 6,000 years ago, and hence it is quite possible
that hemp plants would be grown under similar conditions
and for suitable purposes; moreover, if the hemp
fibre were proved to be suitable for cordage purposes,
it is not difficult to believe that the cultivation of this
important plant in suitable districts would become as
universal as that of flax.
Another reason which suggests the early use of hemp
as a cordage fibre is the universality of its presence in
most eastern countries as a vegetable product. It is at
present cultivated in most European countries, and
especially in Russia, Italy, Austria-Hungary, Serbia,
France and Germany. It is also found on the East
and West coasts of Africa, in many of the States of
America—particularly in Kentucky—as well as in
India, China and Japan.
If the climate is comparatively moist, with a period
of mild temperature and a suitable soil, the hemp plant
can be successfully cultivated for fibre; it is cultivated
in India and in most of the tropical countries for the
production of a liquor which the natives consume in
much the same way as intoxicating liquors are consumed
in temperate countries.
True hemp is a plant which grows wild in Central
Asia, but must be cultivated in practically all other
areas. It is an annual, and requires a rich soil with a
subsoil capable of retaining sufficient moisture to promote
the growth during periods of dry weather. If
otherwise, the growth of the plants would be checked
during this dry period with a consequent deficient yield
of fibre.
With the gradual development of trade, and the
introduction of new kinds of fibre to be used for cordage,
an extended meaning has been applied to the word
hemp, but, unfortunately, the word has been applied
rather loosely to many types of fibre which are used
for rope-making. Thus, one frequently hears the
following names in reference to different fibres—
Manila Hemp,
Sisal Hemp,
New Zealand Hemp,
Mauritius Hemp,
Bowstring Hemp, etc.;
whereas the real hemp is usually designated as—
Russian Hemp,
Italian Hemp,
Indian Hemp,
Sunn Hemp, etc.
To differentiate between these different fibres, and so
provide a better classification and conception of the
terms, it should be clearly understood that the proper
hemp fibres, e.g., Russian, Italian and Indian, are
obtained from the plant Cannabis Sativa, and that the
fibres are located in the bast layers of the plant stems
as exemplified in Fig. 7. The fibres are extracted from
these layers in the same way as the fibres of flax and
jute are extracted from similar layers, that is, by a
process technically termed “retting.” Such fibres are
called soft fibres in contradistinction to hard fibres to
which class Manila, Sisal, New Zealand, Mauritius and
Bowstring fibres belong. The hard fibres are located
in the leaves or in the leaf stalks of plants; typical
examples of the general appearance of such plants and
the internal characteristics are illustrated in Figs. 1 to 5.
CHAPTER IV THE CULTIVATION OF HEMP
The botanical or scientific name for hemp is Cannabis
Sativa, order, Moraceoe, sub-order, Cannaboidae. The
plant grows wild in Central Asia, but is cultivated in
many tropical and temperate regions of both hemispheres.
From a cordage point of view the fibre is,
naturally, of most importance, but, incidentally, it
might be mentioned that the seed is used as a food for
birds, and oil is extracted from it; in addition, in
tropical countries, a resinous juice exudes from the
stalks, leaves and flowers which is made into a violent
intoxicant.
The plants in general attain a height of from 4 to
8 ft. or more, and in exceptional cases, such as under
good cultivation in suitable soil, approach 20 ft. in
height. The leaves are five to nine lobed with serrate
margin. The plants are dioecious and the flowers are
yellowish-green, small and inconspicuous; the male
flowers are numerous and produced in drooping panicles,
each flower of five segments; the female flowers are
fewer in number, on spikes, single leaf, single ovary,
with greyish-green to brownish-grey seed, and rich in
oil. The matured stems are usually hollow, and the
bark layer very fibrous throughout the whole length of
the stem.
The plant readily adapts itself to great changes of
climate, and, as already stated, is found in all climates,
from the tropical ones of India and China to the frozen
regions of Northern Russia. It is adversely affected,
however, in the earlier stages of its growth by frost,
and always requires a moderately strong sunny period
during its growth. It is cultivated in the temperate
climates chiefly for its valuable fibre, but a serviceable
fibre may be obtained from the plants which are grown
in tropical countries.
The most important fibre-producing areas are Russia,
Italy and Austria-Hungary, but it is produced in other
countries, notably those mentioned below, as well as in
Turkey, China and the Southern and Western areas of
the United States of America. The Italian fibre is the
best of all for fine work, while the Russian fibre, which
has a special affinity for tar, is the most satisfactory
for use in the manufacture of heavy cordage for maritime
purposes.
The approximate annual production of hemp from
fourteen different countries appears below—
Russia
400,000
tons
Italy
80,000
„
Hungary
50,000
„
India
36,000
„
Siberia
22,000
„
Austria
18,000
„
France
15,000
„
Japan
8,000
„
Serbia
8,000
„
Caucasus
5,000
„
Poland
4,000
„
Bulgaria
2,000
„
Germany
2,000
„
Roumania
1,500
„
The successful cultivation of hemp requires a rich,
deep and well-worked soil with a large amount of humus.
Alluvial soils are well adapted for the purpose. The
strong loam soils of Italy are typical of the best. In all
cases a good supply of moisture is necessary, otherwise
the crop would be short and stubby and ill adapted for
the production of fibre.
The land should be well prepared by deep ploughing,
and followed by rolling and harrowing to produce a
level and uniform seed bed. The roots of the plants
will penetrate into the subsoil if the land is well
ploughed, but waterlogged land is unsuitable. A liberal
supply of manure is essential owing to the vigorous
growth of the crop, and while farmyard manures are
the best, the stalks of a leguminous crop may be ploughed
in. Manure from animal slaughter-houses is very suitable,
and all refuse from the previous hemp crop should
be returned to the land. Since the hemp fibre contains
a large amount of lime and phosphates, it may sometimes
prove advantageous to use dressings which contain
these substances.
The seed should be selected with care, and should be
tested for its powers of germination. Stored seeds are
liable to heat and lose their vitality, and immature
seeds are also unsatisfactory. Indian and Chinese seeds
are often mixed with home seed. In temperate climates
sowing should take place as early in spring as possible,
but after the night frosts have passed. The early spring
rain and sun are very beneficial, and the foliage which
appears moderately early helps to conserve the moisture
in the soil as the heat of the sun gets more intense.
The amount of seed to be sown depends upon the
type of fibre desired; thus, one bushel of seed per acre
for coarse fibre to three bushels per acre for fine fibre
are the approximate quantities, and the seed may be
sown broadcast by hand, or by machines into drills
about 6 or 7 in. apart. In all cases the seed should be
well covered to prevent ravages by birds, hence, it is
usual after sowing to harrow and roll the fields again
for the above purpose, as well as to prepare a level and
uniform bed for the germination of the seeds.
Where the land is cultivated with the production of
seed as its main object, the seeds should be sown thinly
and wide apart, say, in drills or rows from 6 to 7 ft.
apart, so that the plants will branch extensively and
thus provide facilities for a profusion of flowers. The
male plants are pulled after the bloom is shed, but the
female plants are allowed to mature under the best
conditions so that a large crop may result. Great care
must be taken in harvesting and in storing the seed;
provision must be made to prevent the deterioration
of seed through a process of heating. The average
yield of seed per acre is about thirty bushels, but in
exceptional cases as many as sixty bushels may be
obtained.
Under satisfactory conditions the young plants should
appear in from seven to twelve days, after which it is
necessary to thin them out and to remove the weeds.
While the plants must be wide enough apart to facilitate
good growth, there should not be too much space between
them when grown for fibre, or branching out will
result. If a field has become troublesome with weeds,
no crop will eliminate them as quickly as that of hemp.
If desired both male and female plants may be harvested
at the same time, but it is often considered
advisable to harvest them separately. It is as well to
make most of the mixed crop if the labour is available.
The male plants may be cut or pulled when the flowers
attain maturity or a little after, and when the leaves are
changing colour from green to brown. The female
plants being shorter may be allowed to remain for about
four weeks when the seeds are beginning to ripen.
The yield of fibre per acre of land cultivated is influenced
by several conditions, but on good lands under
satisfactory conditions of cultivation, an average of
6 to 7 cwt. may be relied upon, and in many cases
this quantity is easily exceeded.
After the plants are harvested, a number of minor
operations take place in different districts before the
plants are subjected to the important process of “retting”
or rotting. These preliminary operations are
mostly to reduce the weight of the plants and to discard
undesirable matter which happens to be easily detached,
as well as to secure uniformity. Thus, the tops and
roots may be cut off, and the leaves stripped or beaten
off, while after the plants have been dried, they may
be arranged according to length and thickness. They
are then tied up into bundles of suitable bulk for the
operation of retting.
CHAPTER V RETTING, BREAKING AND SCUTCHING
The retting operation is that process which converts
the constituents of the stems into that condition which
will enable the bast layer, see Fig. 7, to be separated
easily from the remaining parts of the stem. In all
fibrous plants of the type illustrated in Figs. 6 and 7,
a retting process is conducted in which the plants are
either submerged in water, called “water retting,” or
spread on lands adjoining the cultivated areas to undergo
what is termed a weathering action, or “dew retting.”
Water retting is the more satisfactory and gives the
better results, and, in the hands of experienced operatives
a more rapid production of fibre of the better grades.
The submersion of the plants, caused by placing
stones, clods or the like on to the bundles, may be in
slowly-running rivers, in which case the bundles are
kept intact in crates moored to the bank, or a similar
submersion may be conducted in a series of tanks or
ponds. In the latter case a supply of water may be
allowed to enter and leave the tank, and the plants are
kept there until the operation is complete. Stagnant
water acts quicker on the plants than does running
water.
The retting action is a process of fermentation, and
the amount of active bacteria can be regulated by the
temperature and rate of movement of the water. Flax
retting in the river Lys, near Courtrai, is the finest
system known at present, and its value is due to
the slow rate of movement of soft water which is
favourable to the production of the retting bacteria;
the adaptation of a similar system to this where the
water supply is suitable will give high-class results.
Fermentation starts soon after the plants are submerged,
and the rate of fermentation depends upon the
temperature of the air and water; its progress is identified
by the presence of air bells on the surface of the
water. As the operation proceeds, the bundles have a
tendency to rise to the surface, and hence extra weights
are added to keep them submerged. When the formation
of air bells ceases, the operatives carefully examine
and test the stems to ascertain the progress of the
operation; they usually strip off part of the bast layer,
see Fig. 7, from the wood or core, and their judgment
of the correct stage of retting is determined by the ease
with which this separation is effected. Great skill is
required here, or rather ripe experience, for if the retting
is not complete, a portion of the woody matter goes
forward with the fibre, while if the stems are over-retted,
the fibre is weak; in both cases, a faulty judgment
causes trouble in the actual manual or mechanical
processes which follow.
Other methods of retting are adopted in different
countries, and even in certain districts of those countries
where the above system is in vogue. It will be understood
that the choice of any system will depend largely
upon local circumstances, and in all cases, other things
being equal, the method adopted will be that which will
yield the largest quantity of hemp fibre at the least cost.
The characteristics of the fibres are typical of the
countries in which the plants were grown, and of the
processes of retting. It will be almost invariably found
that the best fibre is the result of the most elaborate
and careful methods of cultivation and retting, together
with the equally careful and efficient subsequent
processes of breaking and scutching.
It need hardly be said that the above elaborate and
costly methods are adopted only for the very finest
grades of fibre; they would not be attempted in the
case of those plants which grow and ripen so rapidly
in some tropical countries, and in which a short, harsh
fibre only is obtained; for such plants the cheapest
and simplest methods of extraction are practised.
Many praiseworthy attempts have been made, and
others are still in progress, with varying degrees of
success, to extract the fibre quickly. None has yet
been able to supplant the above-described costly,
lengthy and laborious process, but with modern science,
machinery and experience, one might expect that some
brilliant genius will ultimately solve the problem.
Many industrial problems have been solved by the joint
action of experience and applied science, and one might
therefore hope to see a great simplification of the present
hazardous operation of retting.
The successful introduction of a machine or a system
of machinery which would pull, strip and clean hemp
and allied plants and fibres on the field of growth would
not only open up new fields of cultivation, but would
increase the wealth of our country by millions of pounds;
it would do much to prevent the depopulation of the
rural districts and so help to preserve the hygienic
conditions of our large towns.
The retting operation completed, the stems are
washed and spread on grass land, if available, or stooked
like grain and allowed to dry thoroughly. It is acknowledged
to be advantageous to allow the stems to remain
a few days on the grass, for after this exposure the fibre
is more easily and efficiently separated from the other
constituents of the bast layer.
The ribbon-shaped layer may be about 3 ft. long in
the shorter Russian grades of hemp, but up to 15 ft.
in length in the Italian grades. The colour varies from
grey and brown to a rich cream and almost white in the
finest grades.
The ultimate fibres are large and somewhat irregular
in shape; they vary in length from 0·2 to 2 in., with
an average length of about 1 in., while the diameter is
only about 1/1000 or 0·001 of an inch.
Breaking and Scutching.—Various methods are
adopted to separate the bast layer from the central or
woody part of the retted and dried stems of hemp, but
in all cases the operation thus involved is termed
“breaking.” The central woody part has to be broken
into a great number of short lengths, and this is done
in some districts by exceedingly simple apparatus, and
in other districts by modern breaking machines. Perhaps
the simplest apparatus which is used for this
purpose consists of a series of Δ-shaped wooden bars
arranged horizontally in the form of a grid, and into the
cavities of this row of bars fits another group or series
of similar bars but inverted. The latter group is hinged
at one end and provided with a handle at the other.
When the handle and the upper set of bars are raised,
a few hemp stems are laid across the fixed lower bars;
the handle is then pressed downwards, and this causes
the stems to be squeezed and broken between the two
sets of bars. By repeated blows with the upper bars,
and lateral movements of the stems, it is evident that
the woody core would be broken, and this is done
without damaging the fibrous layer. A treadle may be
attached to the handle end of the hinged grid and thus
leave both hands free to manipulate the stems and to
remove that portion of the broken wood which has not
already dropped through the slots in the lower grid but
remains between the bars of the same.
The mechanical means for this purpose consist of a
number of fluted rollers between which the stems pass
and by the flutes of which the wood is broken. Sometimes
scrapers are used in the same machine to help
to remove the small particles of wood. What remains
in the hand after the simple manual process is completed,
or what is delivered from the machine by the
delivery rollers, are the unbroken fibrous layers to which
still adhere several particles of woody matter or shive
as it is called. A further operation, termed “scutching,”
is necessary to remove this shive and so leave the
lengths of fibre as clean as possible.
Scutching.—The operation of scutching may be considered
in some respects in the light of a scraping action
in which the broken and partially-clean, ribbon-like
structures of fibres occupy a position between a fixed
and a movable board, and are subjected to the friction
between them. The simplest apparatus for this purpose
consists of an upright wooden board with a horizontal
slot near its upper end and through which the
ends of the fibres are passed. The fibres hang downwards,
and while thus depending a flat wooden “scutching
handle” or flail—very similar in shape to a baking
spit—is brought smartly with its edge to traverse downwards
against the fibres, and thus to remove the objectionable
shive but at the same time to prevent, as far
as possible, the destruction of the fibrous layer and the
accumulation of waste. The operative can expose as
much of the fibrous layer as desired to the action of the
scutching handle in virtue of the slot, and after one end
of the “strick” is finished, the other end is treated
similarly.
While the above hand method is largely practised and
is quite satisfactory where comparatively small quantities
have to be treated, or for very fine and expensive
material where delicate treatment is essential, the modern
method of scutching is done by power. The feeding
and manipulation of the stricks are, however, still under
the direct control of the operative. In these mechanical
scutchers it is usual to employ six to twelve handles—narrower
but longer than the hand flail—and these
handles project from a common centre or shaft, somewhat
after the form of the sails of a windmill. As the
shaft rotates, the handles are brought successively to
act against the fibres as in the simpler process.
Large quantities of Russian and other hemps are only
partially cleaned, and are termed “siretz” hemps, while
in some districts where the most valuable plants are
grown, the bast layer is stripped from the stems, and
the material subjected in smaller quantities to the
cleaning and washing processes, thus producing a higher
value fibre.
In hand scutching an operative cleans on an average
about 10 to 12 lb. of Italian hemp per hour, but such
quantities can be, obviously, only approximate, for the
quantities prepared will vary greatly, depending as they
do upon the efficiency of the apparatus at command,
the degree to which the fibrous layer has to be cleaned,
the quality of the material and the skill of the operator.
The better grades of fibre usually and almost invariably
receive more treatment than the lower grades.
The commercial value of hemp depends, as already
stated, upon its strength, colour, freedom from faults,
and its spinning properties; comparative values are
scarcely possible unless in certain seasons, because
prices fluctuate greatly according to the demand for
certain grades of cordage as well as to the prices of
other fibres which may be used for similar goods.
Italian hemp can be spun into thinner or finer yarns
than any of the other hemps, and it is therefore a
competitor with certain grades of flax. French, Chinese
and Russian hemps are also valuable, and besides being
used alone, are sometimes mixed with the coarser
varieties of Italian hemp for certain kinds of cordage
and lines.
The following table shows the amount of fibre in
tons for five years in regard to Russian and Italian
hemp imports to the United Kingdom.
1907.
1908.
1909.
1910.
1911.
Russian
17,299
15,753
13,816
12,576
14,981
Italian
10,462
8,133
10,144
10,298
10,343
27,761
23,886
23,960
22,874
25,324
CHAPTER VI THE CULTIVATION OF PLANTS FOR HARD FIBRES
The different types of hard fibres for cordage are mentioned
in Chapter III, page 17, and, although there are
certain features which are more or less common to all,
there are differences which make it advisable, if not
necessary, to discuss each main type separately.
One of the best-known hard fibres is the Manila or
Abaca fibre (obtained from the wild plantain, a variety
of the banana plant) Musa textilis. It is an excellent
cordage fibre and is largely used both in this country
and in the United States of America. The plant, from
which the fibre is obtained, is in many respects indistinguishable
from the banana plant during the period of
growth; the colour of the leaves of the banana plant
is, however, usually of a darker green shade than that
of the leaves of the Musa textilis, while the flowers
and fruit of the banana are much more abundant than
are those of the Manila plant. On the other hand, the
fibre of the banana plant is very poor in quality, and
practically valueless for cordage purposes.
The Musa textilis is peculiarly indigenous to the
Philippine Islands, indeed most of the attempts to
cultivate this plant in other areas have been unsuccessful.
Manila, Luzon and Cebu are three of the principle fibre-producing
areas, and, because of the suitability of the
soil and climate in these areas, the growth of the Manila
industry has been extensive, and large quantities of
high-grade fibre are produced annually in these three
areas.
Cleared forest land is very suitable for the propagation
of young plants which require a certain amount of
shade to assist their growth in the early stages. During
the period of growth a large number of suckers or young
plants grow around the parent plant; these suckers
are used in general to start a new plantation, while in
other cases the young plants are raised from seed. In
both cases, the young plants are set out so that from
500 to 600 may occupy an acre, and the distance
between the plants is from 8 to 10 ft. If plants
are propagated from seed it takes about one year
before the shoots can be set out in the plantation,
and they should be spaced in the same way as the
suckers.
The ground should be kept clear of weeds at least
during the first year; after this period, vigorous growth
starts, if the usual moist season prevails, and during
the three or four years of growth the plant attains a
height of 8 ft. and upwards. Occasionally a plant
grows to a height of 20 ft. After the lapse of three to
four years, the fibre plant develops a flower, and then
the plant should be cut down to obtain the best type
of fibre.
Hilly land, and particularly volcanic slopes with a
moist loose soil, are very well suited for the cultivation
of these plants. Swamp lands, while satisfactory for
certain types of plants, are unsuitable for the cultivation
of Manila.
The work of harvesting and the extraction of the
fibre are usually done on the contract system; a supervisor
will take over the plantation upon which he starts
his men on the dual process.
The fibre is produced in the sheathing leaf stalks
which form a bundle 6 in. to 1 ft. or even more in diameter
with a central stem or flower stalk about 3 in.
in diameter. The flowers are near the upper part
which may reach a much greater height than the
leaves. The pistillate flowers are nearest the base
and form fairly large fruits which are filled with black
seeds.
The bundle of sheathing leaf stalks are cut off a few
inches above the ground and split up into widths of
about 5 to 6 in., after which the fibre can be extracted
either by hand or by machine. When the hand method
is practised, the stalks are first well beaten with wooden
mallets, and then scraped with suitable instruments
until the fibre is freed from the surrounding vegetable
matter. The separated fibre is finally washed and
dried, and made up into bales of 280 lbs. each.
It is very important that the substances which surround
the fibres should be completely removed, and
that the fibre should be thoroughly dried after it has
been well washed. These operations completed, the
dried fibre is conveyed to the premises of the owner of
the plantation to be selected and valued. The approximate
cost of extracting the fibre is half its market
value, and this sum is often paid by the farmer to the
men who perform the work.
The stripped and cleaned fibre is now graded by
experts who are appointed by the Government of the
Islands, and the various qualities are now much more
uniform than they were formerly, see page 34.
In general, a yield of 2 to 3 lb. of fibre per plant is
obtained, but this quantity may be doubled in some
cases. With the average mentioned, approximately
12 cwt. of fibre per acre would be produced, but a considerably
higher quantity could be obtained by more
perfect machinery, as the loss of fibre in the operation
of stripping amounts, in many cases, to 25 per cent.
of the possible production.
The following table shows one method of grading the
fibre, and the average price per ton during June, 1915.
See also page 51.
Extra Fine Prime
£56
to
£58
Prime
52
„
54
Superior Current
50
„
52
Good Current
48
„
50
Midway
44
„
46
Current
41
„
42
Seconds
38
„
39
Brown
36
„
38
Fair
37
„
38
Medium
32
„
33
Coarse
28
„
29
Coarse Brown
27
„
28
Another method of grading is by means of letters,
and Fig. 10 is a photographical reproduction of fifteen
different samples representing the general grading and
marked A to M. There are also a few intermediate
grades which are of similar classes of fibre but
discoloured—a fault due to imperfect cleaning.
Fig. 10 MANILA FIBRES: ORDER OF GRADING
The imports of Manila to the United Kingdom for
the years 1911 to 1915 inclusive and the actual value
appear in the following table, while the average value
of one grade, Fair Current, appears alongside. See
also page 34.
Year.
Tons.
Total Value.
Price per ton of Fair Current.
1911
75,449
£1,647,542
£19 — —
1912
83,313
£1,990,481
£21 10 —
1913
64,579
£1,600,450
£34 — —
1914
54,206
£1,396,593
£27 15 —
1915
57,783
£1,760,471
£28 10 —
Sisal.—This is a fibre which is almost of equal
importance to Manila for the production of cordage.
The plants, which are produced extensively in Mexico,
Africa and the Bahama Islands, form a group termed
the Agaves.
Those plants which are most extensively cultivated for
fibre purposes have recently been classified, see page 8.
The particular Agave plant from which the Sisal
fibre of commerce is obtained is the Agave Sisalana, or
Henequen, natural order, Armaryllidaceae, the chief
centres of production of which are Yucatan and Campeachy;
the cities of Merida and Progresso are the
centres of production of the fibre for the export markets.
The plants grow very successfully on waste and arid
lands, and require very little attention after the preliminary
operations of clearing the land and of planting
out the young Agaves either as bulbules or “bulbils”
produced from the creeping roots.
The stems of the plants are stumpy, and large fleshy
leaves are produced which attain a height of 3 to 6 ft.
The flowers are produced on a long stalk or pole which
often rises to 30 ft. or more. The flowers appear in
dense groups on lateral branches upon the axils of which
develop bulbils; these grow to maturity and then drop
to the ground where many of them take root and thus
provide young shoots which may be replanted for
another crop.
In the formation of new plantations for the production
of fibrous plants, it is only necessary to clean the
ground and dig the soil round where the young bulbils,
suckers, or a mixture of both, are to be planted. They
are so arranged that there is a greater space between
the rows than there is between the plants in a row,
say in the proportion of 8 to 6, and about 1,000 plants
are spaced in an acre.
If the plants are taken from nurseries where the
bulbils have been propagated for transplanting, it may
be found advantageous to provide light tramways for
their conveyance, as well as for the conveyance of the
mature leaves in the opposite direction. The extra
space between the rows is for facilitating such work by
rails and other means. In fact, a plantation for the
cultivation of Sisal plants and the production of the
fibre should be laid out on a definite plan with provision,
not only for successful cultivation, but for the subsequent
operations of stripping, washing, cleaning and
baling the fibre, while a desirable, if not absolutely
necessary consideration, is the choice of ground in close
proximity to a satisfactory district for labour.
A short time after the plants have been set it is
advisable to clean and weed the ground periodically
for at least two years to give the plants a favourable
start; afterwards vigorous growth occurs, and no
further attention in this line is necessary.
It will be evident that a more vigorous growth will
obtain in warm climates than in cold climates, but at
the same time these warm climates may be exceptionally
suitable; indeed, it has already been proved that, in
some of the more recently-established centres of cultivation
such as Africa, a better fibre is being produced
than in some of the older established centres, and,
moreover, the growing period is shorter.
To make a fibre-production area a success, it is
advisable to adopt a systematic extension of the plantation
each season, so that a continuous supply of
leaves will be obtained, and that the available labour
supply can be fully utilized either with operations in
cultivation or fibre extraction; in this way a regular
supply of fibre could be placed on the market for
manufacturing purposes.
After a plantation is completed, the first cutting of
the leaves may take place in from two to four years,
depending upon the situation of the plant and its state.
It is not necessary to cut down the whole plant; the
larger leaves are cut when at maturity, and others as
they mature; successive cuttings may be at intervals
of approximately six months, after which the plant
may be cut down and the spot allowed to remain fallow
for a year, when a new plant is introduced.
The yield of fibre from the plants will vary considerably
from time to time, such variation being influenced
by the district, the weather and by the degree of perfection
of the methods employed for extracting the
fibre from the leaves.
The usefulness of the Agave fibres has been acknowledged
for some time, and their value has been enhanced
by the production of superior fibres in various centres
of Africa as already stated; improved methods of
cultivation and the use of modern and efficient stripping
and cleaning machines may lead to the production of
this type of fibre which will compete successfully with
many of our most valued fibres for cordage use.
As the leaves are cut down from the plants, they
should be removed at once to the stripping machine.
The original name for such a machine was “Raspadore,”
and supposed to be an invention of a Franciscan friar.
The modern English word for the purpose is “Decorticator,”
and, although the term “leaf-crusher” or
“scutcher” appears to be more in keeping with the
operation to be performed on Sisal leaves, than that
of “decorticator,” a more extensive meaning has been
given to the latter term which is now taken to indicate
the mechanical operation for the separation of the
pith and surrounding vegetable structure from the
fibrous layers in practically every type of plant.
Two distinct machines, one for crushing the leaves,
and the other for finishing the stripping, are made by
Messrs. David Bridge & Co., Ltd., Castleton, Manchester,
and these provide an excellent system for treating the
leaves as they are delivered from the field of growth.
By permission of Messrs David Bridge & Co., Ltd. Fig. 11 BRIDGE’S “ACME” GRAVITY PATENT SISAL BREAKER
The crushing machine, termed Bridge’s “Acme”
Gravity Patent Sisal Breaker, is illustrated in Fig. 11.
The leaves of the plant are placed on the travelling
endless cloth between the wooden side guides on the
right-hand side of the illustration. They ultimately
come into contact with the first pair of corrugated
rollers which are so set that there is a minimum of
¼ in. between the surfaces of the opposing corrugations.
After the leaves have been crushed between these
rollers and carried forward by them, they pass between
a second but smooth pair of rollers the nearest distance
between the surfaces of which is 3/16 in. On emerging
from these rollers, the leaves pass down the delivery
table on the left. The upper roller in each pair is
acted upon and pressed downwards by spiral or coil
springs which not only yield slightly to the varying
thicknesses of the leaves, but which will allow the roller
to rise fully ⅞ of an inch in case any foreign substance
should enter between the rollers.
By permission of Messrs David Bridge & Co., Ltd. Fig. 12 BRIDGE’S “CLIMAX” PATENT SISAL DECORTICATOR
The crushed ribbons from the foregoing machine are
now taken to Bridge’s “Climax” Patent Sisal Decorticator,
illustrated in Fig. 12. As in the crushing machine,
the material is fed into the rollers by an endless cloth;
the ribbon-shaped lengths are exposed to the action of
opposed drums on the same principle as that embodied
in the original raspadore, the result being that the
remains of the objectionable matter which accompanied
the fibrous layer from the crushing machine is scraped
off and a maximum amount of fibre delivered. The
Decorticator is provided with all the latest improvements
for a maximum production, and both machines,
together with the washing tanks, Fig. 13, and the
necessary power plant for driving the whole system can
be housed in or near a simple structure somewhat as
illustrated in Fig. 14.
By permission of Messrs David Bridge & Co., Ltd. Fig. 13 WASHING TANKSBy permission of Messrs David Bridge & Co., Ltd. Fig. 14 HOUSING FOR POWER PLANTBy permission of Messrs David Bridge & Co., Ltd. Fig. 15 CUMMINS’S PATENT HORIZONTAL HYDRAULIC BALING PRESS
The fibre, having been extracted, washed and dried, is
conveyed to the rapid baling press, Fig. 15, which is an
illustration of Cummins’s Patent Horizontal Hydraulic
Baling Press. Here the fibre is packed by hydraulic
pressure into a small space ready for exportation to
those countries where the fibre is to be manufactured.
The above type of baling press is now largely used,
not only for Sisal fibres, but also for China jute, cotton
and other textiles, and it is capable of compressing the
fibre to a density of 60 lb. per cubic foot.
After the third year’s growth, the annual production
of fibre reaches about one ton per acre. The production
of fibre from the various countries has been greatly
increased during recent years, and that for 1914, which
will be found in the table on page 52, may be taken as a
good indication of the quantities placed on the market.
There has not yet been any considerable competition
between Sisal and Manila fibres for the manufacture of
similar types of cordage, but with improved methods
of cultivation and of cleaning the Sisal product, a
greater competition may be expected.
A large quantity of Manila fibre is used in this country
for binder twine, whereas Sisal is used for the same
purpose in the American centres. As a matter of fact,
the U.S.A. markets of different kinds absorb 90 per
cent. of the total Sisal crop which amounted in 1914
to 220,000 tons.
A new method of marketing the Sisal fibre from
Yucatan has been introduced through a Committee or
Commission who will be responsible for the grading
and marketing of the fibre and will, with the sanction
of the Government, deal entirely with the financial
arrangements.
The Commission will receive all the graded fibre,
and on receipt of this a payment will be made to the
farmer. The fibre will be placed on the market at
current rates, and every five years the accounts will
be balanced and the surplus, if any, will be divided
pro rata amongst the producers. In the case of loss,
the deficit will be met by the Commission.
Sisal fibres are graded as under—
Special: perfectly clean and absolutely white fibre,
free from stains or adherent pulp.
Superior Clean: perfectly clean fibre of creamy or
yellowish tint, free from stain or pulp.
Current Clean: well scraped, whitish or greenish
colour, 5 per cent. dust permitted. This is the standard
grade for price.
Stained: also well scraped but with dark or red
streaks. No more than 25 per cent. dark and no
adherent pulp.
Inferior Stained: must be free from adherent pulp,
but may contain as much as 75 per cent. of dark fibres.
New Zealand Hemp or Flax.—The botanical name
of this plant is Phormium Tenax, natural order, Liliaceae.
The plant has long, peculiarly-shaped leaves, the roots
of which send out creeping rhizomes on which the leaves
6 to 10 ft. in height, are produced in clumps. Maturity
is reached in about four years, and propagation is
obtained by the growth of the rhizomes, and also by
the self-sown seeds which are produced in large numbers
from the flowering and fruiting stage.
Large quantities of this useful fibre are used, and it
can be produced cheaply and in large quantities from
otherwise unproductive lands, such as the drained
swamp lands in the neighbourhood of the Manawatu
river in New Zealand. In this district the plants grow
in dense masses, and although more than 20,000 acres
are under cultivation, additions are gradually taking
place. Through this area are laid about fifty miles of
light railway tracks. The plantations require little
attention beyond that of careful drainage; over-drainage
may cause as much damage as under-drainage.
Wellington is the principal shipping port, but shipments
are also made from Auckland and other ports when
the value of the fibre makes such a course profitable.
Phormium Tenax has also been cultivated on a comparatively
large scale in St. Helena, and the results,
both financially and otherwise, are satisfactory. The
selected lands in this island are now well drained, and
tramways are laid for the rapid conveyance of the
leaves after they are cut down to the stripping mills.
Sometimes aerial railways are used when a river has to
be negotiated. It will be quite well understood that a
cheap and rapid transport is a desideratum.
Only well-matured leaves must be cut down, and
these are conveyed to the stripping mills; in the
Manawatu district of New Zealand about fifty such
mills are in existence, and the introduction of improved
machinery for this stripping operation will certainly
lead to the extension of the cultivation of these plants
and to the after processes.
Much has been done to introduce an efficient machine
for stripping the leaves, and many premiums have been
offered by the New Zealand Government for a perfect
machine. One now under trial gives promise of good
results.
The greatest difficulty in connection with the stripping
of Phormium Tenax leaves is due to the peculiar
shape of the lower end of the leaf. A very deep midrib
extends for some distance and gets more pronounced as
the lower end of the leaf is reached. A large quantity
of the fibre is collected in this rib, the shape of which
makes it difficult for mechanical parts to treat successfully,
and necessitates a larger amount of labour than
in the case of straight or flat leaves of the ordinary
type.
In former methods of stripping and cleaning it was
found necessary to paddock and bleach the stripped
fibre, but the claims of the new invention, if sustained,
will render these processes unnecessary.
The production of the fibre may reach 13 cwt., and
2½ cwt. of tow per acre during the life of the plants,
while the stripper can produce from 20 to 25 cwt. of
fibre per day.
The colour of the fibre is light yellow to brownish,
but it is rather soft and dirty at the top end. It is
graded as below—
91
to
100
marks
=
Superfine,
81
to
90
„
=
Fine,
71
to
80
„
=
Good Fair,
61
to
70
„
=
Fair,
51
to
60
„
=
Common.
Other Fibres.—The chief hard fibres are augmented
by the use of the “Maguey” plant which is cultivated
largely in the Philippine Islands in districts bordering
on the Manila centres, while Mauritius fibre is produced
largely in the Islands from an Agave, the Furcroea
Gigantea, order, Amaryllidaceae, known in Mauritius as
“Aloes.” The plant, see Fig. 16, is somewhat similar
to the Sisal plant, while the fibre obtained from it is
of a soft nature, and is usually sent to this country in
an imperfectly-cleaned state. The dust which accompanies
the fibre emerges from it in the processes of
manufacture, and is very disagreeable to the operatives.
Owing, however, to its good light colour, and the softness
and pliability of the goods made from it, the fibre
is often preferred to the other hard fibres for certain
types of work.
By permission of Messrs David Bridge & Co., Ltd. Fig. 16 MAURITIUS FIBRE PLANT
Coir.—Coir fibre is obtained from the husks of cocoa
nuts. The extraction of the fibre from these nuts forms
native industries in many parts of India and Ceylon.
The husks are soaked in water for a time, and then
beaten with sticks or mallets; the separated fibres are
then dried and spun by hand with the aid of very
simple appliances. Afterwards, two of these single
yarns are combined or twisted together to make what
is known as two-ply or two-fold twist. The twist is
then made up into short lengths, rolled into small hanks
and baled for export. Of later years, much longer
lengths have been made and done up into coils, while
small “dolls” or rolls are made up for sale in small
quantities, particularly for use on farms.
Coir fibre has been very widely used for many purposes
in the rope and cordage trade, principally for the
manufacture of mooring ropes, spring ropes and lashing
cords, while large quantities of the imported yarns are
used for matting and farming purposes.
It is a very useful fibre when properly made up, and
is of great importance for purposes where it is necessary
for the manufactured article to be exposed to variation
of climate and to wet, while the life of the manufactured
article is greatly extended if it is steeped in oil.
Sunn Hemp (Bengal Hemp).—Sunn Hemp or Crotalaria
Juncea, natural order, Leguminosae, is used on a
smaller scale and for certain goods such as cheap grade
ropes and box cord. The plants grow in several parts
of India, e.g., near Bengal, Allahabad and Benares in
which the cheaper grades are produced, and in some
districts of Western Bengal where a better class of fibre
is obtained. All are of the same family, the difference
being due to the variation of the soil and the method
of retting. (This is really a bast fibre, but it is used
almost solely along with the hard fibres.) The fibre is
harsh and very irregular in the lower grades; in the
better grades it can be used to mix with other fibres
for the production of tow yarns.
The other hemps obtained from India, particularly
from Madras, are not so high grade as to warrant them
being used alone to any great extent, so it is usual to
mix them with other low-grade hemps of higher tensile
strength, or these Indian hemps may be combined with
scutching and hackling tows. The scutching and
hackling tows are sometimes used to produce twines
and cords suitable for box cords and for parcel tying
yarns.
China Jute.—Although this is a bast fibre, its use
is mostly confined to purposes for which the hard fibres
are applied, and hence its introduction amongst them.
It is a product of Hankow and Teintsin in China, and
is largely imported to Great Britain. When suitably
treated it forms a satisfactory fibre for the manufacture
of box cords or similar goods where great tensile strength
is not essential. The fibre is of a good light colour,
and little or no waste is incurred in its transformation
into cordage.
The following details of the production of fibres and
relative costs are given so that the normal values, as
well as the normal quantities may be judged, and also
compared with the abnormal conditions which have
prevailed during the great world’s war.
Italian and Naples hemp is imported to these
islands in large quantities as will be seen from the
following particulars for ten seasons—
Season.
Italian.
Naples.
1903-04
62,000
tons
28,000
tons
1904-05
40,000
„
23,000
„
1905-06
12,000
„
27,000
„
1906-07
58,000
„
30,000
„
1907-08
58,000
„
31,000
„
1908-09
41,000
„
20,000
„
1909-10
55,000
„
24,000
„
1910-11
50,000
„
27,000
„
1911-12
33,000
„
30,000
„
1912-13
58,000
„
31,000
„
10)
467,000
10)
271,000
46,700
average
27,100
average
Average
price
P.C. Italian, £39 11s. 3d. per ton
„
„
P.E. Naples, £41 9s. per ton
„
„
F.S.P.R.H. Russian, £31 17s. per ton
The prices since these dates have gradually increased,
and the present prices are approximately as under—
P.C., Italian
£190
per
ton
P.E., Naples
£200
„
„
F.S.P.R.H., Russian
£170
„
„
China Hemp
£154
„
„
The following table illustrates the grading of Manila
fibre for June, 1917, together with the number of bales
for that month, and the percentage quantity of each
grade. In addition, the last two columns give the
prices; that for 1917 is the market price, while that
for 1918 is the controlled price. Fig. 10 might be
studied along with this table.
Grade Letter.
Grade.
Bales.
% of Total.
1917. Market Price per ton.
1918. Market Price per ton.
A
Extra Prime
899
0·7
B
Prime
2,182
1·6
C
Superior Current
6,852
5·0
£150
£155
D
Good Current
10,020
7·3
£145
£150
E
Midway
17,358
12·7
£135
£135
S¹
Streaky 1
1,865
1·4
£130
£130
S²
Streaky 2
3,937
2·9
£120
£120
S³
Streaky 3
2,935
2·1
£115
£115
F
Current
22,284
16·3
£125
£130
G
Seconds
3,908
2·8
£115
£115
H
Brown
1,886
1·4
£105
£105
I
Good Fair
12,791
9·3
£120
J
Fair
13,561
9·8
£85
£100
K
Medium
4,226
3·1
£80
£95
L
Coarse
12,780
9·2
£78
£93
M
Coarse Brown
5,140
3·7
£76
£80
DL
Coarse
7,153
5·2
£75
£75
DM
Coarse Brown
4,306
3·2
£73
£73
OYT
3,159
2·3
137,242
100·0
The standardizing of the grades has been rendered
necessary by the large amount of inferior fibre which
was being produced, and by the irregular baling of the
fibre. The gradual improvement of the fibre as a whole
may be gleaned from the undermentioned particulars of
the number of bales which were graded into four of
the lowest types. These numbers referred to what
were allocated in August and September, 1917,
and it will be seen that there was a much smaller
percentage of these low marks in September than
in August.
Grade.
Bales: August.
Bales: September.
L
10,548
7,462
M
4,553
3,201
DL
5,775
2,960
DM
2,290
952
23,166
14,575
The shipments of Manila and other fibres for six
years, 1910 to 1915 inclusive, appear below—
Year.
Manila bales.
Mexican Sisal bales.
New Zealand bales.
Mauritius bales.
1910
1,272,000
582,142
103,750
9,990
1911
1,332,297
713,008
96,850
9,161
1912
1,466,110
859,000
96,360
8,697
1913
964,000
876,000
140,445
14,404
1914
943,000
982,000
98,510
8,947
1915
1,160,440
950,000
116,100
6,838
The three columns in the following table show the
prices which ruled in 1915 and 1916 and the current
prices for 1918.
Type of Fibre.
1915.
1916.
1918.
£
£
£
P.C. Italian Hemp
55
90
190
F.S.P.R.H. Russian Hemp
—
—
170
China Hemp
—
—
154
Manila (Fair)
37
54
100
New Zealand Hemp
32
86
99
Mexican Sisal
28
77
97
Java Sisal
—
95-100
99
Mauritius
—
70
95
Maguey
30
70
74
The controlled Government price (U.S.A.) for Sisal
fibre for June (1918) is as follows—
19
cents
per
lb.
for fibre
23
„
„
„
for 500 feet of binder twine
Since one sheaf of corn requires about one yard of
twine, and since the expected requirements for the
Continent of America are 200,000 tons of binder twine,
it follows that this weight of yarn will provide the
binding material for 71,680,000,000 sheaves—almost an
incredible quantity.
Fig. 17 BALES OF MANILA, NEW ZEALAND AND SISAL FIBRES
(b) New Zealand Hemp with ropes made from New
Zealand fibre.
(c) Sisal Hemp with wire.
CHAPTER VII THE PREPARING AND SPINNING MACHINERY FOR HEMP AND OTHER SOFT FIBRES
Since there is such a great variety of ropes, cords and
twines, not only in regard to diameters, but also in regard
to the different fibres used in the manufacture of these
goods, it is not surprising to find that there are many
different kinds of machines involved in the various
operations; some of these machines are introduced
for the special purpose of reducing the fibres to practicable
lengths, but these machines are, of course, used
only for the type of fibres which exceed about 36 in.
On the other hand, it is sometimes found desirable to
cut certain types of fibres which do not exceed the limits
demanded by the capacity of the machines, but this is
done only as a selective operation to obtain the best
and strongest part of the fibre.
While certain classes of soft fibres such as Russian,
French, Chinese and Indian hemps may be used without
any previous hackling operation in the spinning of certain
sizes of cordage, it is found that Italian, Serbian,
Roumanian and Neapolitan hemps must be cut into
suitable lengths and hackled before they can be passed
through the preparing machines; in these latter
machines the fibres are arranged into a practicable
condition before they are subjected to the actual
spinning operation.
The production of yarn for use in the making of
cotton driving ropes involves the use of the whole system
of cotton-spinning machinery, while, on the other hand,
hemp yarns, besides being prepared mechanically, are
still produced by a series of the simplest and oldest
methods of hand hackling and hand spinning.
Fine ropes and twines may be, and often are, produced
by an elaborate system of machinery, and modified
forms of such a system, in which a smaller number
of machines are employed, may be adopted for the
spinning of the heavier yarns.
A complete plant for the manufacture of these yarns
from soft fibres would include the following—
Softening Machine,
Cutting or Breaking Machine,
Hackling Machines,
Spread Boards,
Drawing and Doubling Frames,
Roving and Gill Spinning Machines,
Automatic Spinning Machines,
Throstle Spinning Machines.
The yarns employed may be as small as 60’s for the
finer sizes and as thick as 18’s for the heavy or common
sizes; the significance of this yarn numbering will be
explained later.
In order to have some definite purpose in view, let
it be assumed that it is necessary to make a high-class
rope from Italian hemp; the fibre to be used must, of
course, be of a good quality of cordage hemp. When
the bale of hemp is opened, the fibre will be found to
be in “heads” or “stricks,” that is, collected into
groups with a girth of from 8 to 12 in., and to be from
7 to 12 ft. in length and sometimes even longer.
The first operation is that known as “softening,”
which makes the fibres, as the name of the operation
indicates, more supple, and hence better adapted for
undergoing the subsequent operations. Different
makes of machines are in use for softening the fibrous
material, the chief feature in each machine is that
the heads or stricks of fibre are squeezed between
fluted rollers.
In one type of machine the end of the strick is passed
between the first pair of blades of an Archimedean screw,
then between the fluted rollers of which there may be
three, and its end brought round and joined to the
other end of the strick; in this way an endless band of
fibres is formed. The fluted rollers act as indicated,
and at the same time the Archimedean screw gradually
conveys the endless band of fibres from one end of the
screw to the other end, each slight movement causing
the fibres to enter between the fluted rollers at a different
place. This type of machine, which is, however, rather
dangerous for certain classes of workers, is considered
quite efficient and satisfactory by many spinners, but
the machine which is most extensively used is known
as a “reciprocating softener,” and is made by such
firms as Messrs. Reynolds and Messrs. Combe Barbour,
both of Belfast, and by Messrs. Lawson of Leeds.
The action of the rollers of the reciprocating softener
is rather complicated, for, in addition to the usual
method of rotating in one direction for the sake of
delivering the material, the rollers are moved bodily
forwards and backwards a short distance alternately.
The multiplicity of motions has for its aim that of
subjecting every particle of the strick as much as
necessary to the softening action of the flutes; the
effect of these operations on the hemp is quite evident
when the stricks emerge from the delivery end, for the
material is much more pliant than when it entered, and
is in such a condition that it may be greatly refined
in the subsequent operations.
In this machine the forward motion of the rollers is
obtained by a special arrangement of gearing from the
pulley shaft which extends through the machine and
carries a further belt pulley at the other end. A belt
from the latter pulley drives by means of another pulley
an upper shaft, while a further belt connection from a
pulley on this upper shaft conveys motion to a pulley
running on a stud projecting from the main frame.
Compounded with the latter pulley is the speed change
pinion, and a train of gearing, consisting of four pairs of
compound wheels, conveys the desired motion to the
fourteen pairs of fluted rollers which are arranged in
two concentric semicircles in the upper part of the
machine. The centre of these concentric semicircles is
the central shaft of the machine, and on this shaft is
placed the pinion and wheel of the second compound.
Near the ends of this central shaft, and close to the
outer part of the two main frames, swings two substantially-constructed
brackets; each bracket has two
horizontal arms from each of which a short shaft projects
to carry a wheel and pinion, while the extreme
lower end of the bracket is attached by means of a
connecting rod to a crank placed on the large wheel
below, and driven from, the main pulley shaft.
As indicated, this mechanism is duplicated, one set
on each side of the machine. The object of the small
pinions on the horizontal arms of the swinging brackets
is to drive the fourteen pairs of fluted rollers through
the medium of two large wheels, one on each side, each
wheel being provided with internal teeth. The object
of the cranks and connecting arms to the said brackets
is to cause the fourteen pairs of rollers to reciprocate.
This reciprocation adds to the effective softening of the
stricks by rotating the material for a longer time in
the machine, and thus repeating the softening effect of
the rollers on different parts of the fibrous material.
After the stricks have been efficiently softened in one
or other of the machines mentioned, they are conveyed
to the cutting or breaking machine which is adapted to
sever the stricks into lengths suitable for treatment in
the hackling machine.
By permission of Messrs David Bridge & Co., Ltd. Fig. 18 BREAKING MACHINE
These cutting or breaking machines are of two distinct
types—
(a) Those in which the fibres of the stricks are torn
asunder; and
(b) Those in which the fibres are broken by the action
of what are known as “cutting wheels.”
A good example of a machine which tears or breaks
the stricks is that illustrated in Fig. 18, and made by
Messrs. David Bridge & Co., Ltd., Castleton, Manchester.
The machine is of substantial construction, but experienced
operatives are required to take charge of it.
One end of the softened strick is wrapped round the
back fixed square bar to the left of the illustration;
then about two turns of the strick are wrapped round
the front square bar which rotates when the attendant
presses down the foot lever near the floor. Since the
revolving bar has a tendency to carry the strick round
with it in virtue of the movement given to it by the
train of wheels from the motive part, it follows that
ultimately the stretch of fibres between the two square
bars will be broken, and then the operation is repeated
with the remainder of the long strick. The friction
clutch, on the right of the three pulleys, and the main
shaft are revolving continuously while the belt on the
middle pulley is in motion, but the friction pulley itself
moves only when the friction clutch is expanded due
to the downward movement of the foot lever which,
at the same time, releases the brake on the left pulley
of the three. When the foot is removed from the foot
lever or treadle, the clutch fork slides the clutch on the
shaft and breaks the contact between the friction clutch
and friction wheel; simultaneously the brake grips its
pulley and thus arrests the wheels and the rotating
square bar.
The cutting or breaking type is designed on quite
different lines from the above machine, and a very
popular and efficient machine of the former type is
known as the “Revolving Cutting Machine.” A series
of round pins (sometimes V-shaped teeth) project from
the face or periphery of a large central revolving wheel,
and on each side of this wheel, and at a suitable distance
from it, is a pair of slowly-moving rollers which are
grooved on their circumferences to intersect with each
other and so grip or hold the material as it is being fed
to the pins of the cutting wheel. The operative cutter
stands in front of the machine with a long strick of
hemp in his hands. He grips the strick at two convenient
places, and, having decided upon the point
where the piece should be cut or broken, he arranges
for this point to pass into the machine midway between
the two pairs of feed or retaining wheels. The machine
is made in duplicate so that the same cutting, or breaking
wheel may serve for both, but each operative has,
naturally, his own set of feed wheels.
As already stated, the lengths of the pieces when
broken or cut will depend upon the type of hackling
machine in which the severed lengths are next to be
treated, and also upon the particular class of rope into
which the fibres are to be spun. The usual length
limits are 24 in. and 30 in., although conditions might
arise in which it is desirable to go beyond the extremes
of these common lengths.
The suitable lengths of cut material are now made
up into convenient sizes or bunches and conveyed to
the machine hackling department.
Certain classes of Russian, French, Chinese, Indian
and Italian hemps may be considered in common in all
subsequent operations, and, in general, will require most
of the treatment which is given to the specific case of
Italian hemp under discussion.
By permission of the Edinburgh Roperie Co. Fig. 19 HACKLING MACHINE
The hackling machines which are used in modern
cordage or rope walks are similar to that reproduced in
Fig. 19. In this particular machine there are sixteen
different holders with pieces of hemp fibre depending
from each, the lowest visible part of the fibre being on
the same level as the uppermost part of the hackles or
tools. The visible parts of the latter extend to a point
in line with the waist of the attendant. There are four
sections of tools in the full width, and each section is
made up of four sets, while each set contains twenty-four
tools, the whole arranged in a closed path so that
while they rotate, the pins in the tools may act upon
the pieces of hemp as the latter move in a vertical plane
under the influence of what is termed the “head” of
the machine.
The number of tools vary according to the accommodation
available in the department devoted to this
section of the work. The tools are fixed to a series
of bars which in turn are riveted to a set of leather
sheets, the whole being rotated as indicated by means
of carriers which are arranged on two shafts with
suitable fixings.
In the “head” the necessary mechanical parts are
placed for moving the holders, and therefore the pieces
of hemp, collectively and intermittently along what is
known as the “channel.” The inclined rod, immediately
under the name plate of the machine, with its
additional parts convey this motion to each of the
holders. In this manner, each holder, with its complement
of hemp, is moved in regular succession opposite
each of the sixteen sets of hackles or tools, and therefore
passes from one end of the machine to the other.
This movement takes place when the hemp is at or
near its highest point. As each holder reaches the end
of the machine, it is removed from the channel, the
bolt of the holder unscrewed, the plate removed, and
the piece of hemp turned end for end. After this the
plate is again placed in position, the nuts screwed tight,
and the holder entered into a similar channel on the
other side of the machine, but with the undressed end
of hemp downwards. A very similar movement is now
imparted to the holders at this side of the machine so
that the same process of hackling as that performed
already may be imparted by an identical group of tools.
The work is, of course, continuous in this respect that
the girl or boy is almost constantly engaged with the
attention of the holders as they reach the end in regular
short periods of ten to fifteen seconds. The hemp
ultimately reaches the end of the machine from which
it started, but in a different plane, and is withdrawn
from the holder to be replaced by an undressed piece.
Until a comparatively short time ago all the above
operations of feeding were done by hand as explained,
but most modern hackling machines have now attached
automatic mechanism for performing these functions.
The machine in Fig. 19 is provided with this automatic
screwing and unscrewing mechanism. One attendant
introduces the pieces of hemp between the plates of the
holder when such plates have been separated by the
apparatus, but from this point all the operations, including
the removal of the holder, the turning of the piece of
hemp, the unscrewing and screwing of the nuts, and
the insertion of the holder with the unhackled ends
downwards into the second channel, are performed by
this ingenious group of automatic machinery. The
design of such machinery differs with different machine
makers, but very similar principles are embodied in all.
The ends of the hackling machine frame are in all cases
substantially made so that all parts may give the
minimum amount of trouble in actual work.
The size of the pieces which are held by the holder
and acted upon by the tools during the operation of
hackling will depend upon the class of yarn to which
the fibre has to be spun. As a general rule, the pieces
for rope and twine yarns are arranged so that there
are two to four per pound; in other words, the pieces
are from ¼ lb. to ½ lb. each. It must be remembered
that the finer the quality of yarn desired, the more
hackling must take place, and hence it will be necessary
to use a hackling machine with finer tools, and also to
employ more tools in a row.
As a general rule the best yield of fibre is obtained
when the maximum number of tools are used, but at
the same time it is necessary that the grading of the
pins or hackles in such tools should be judiciously
chosen in order that the splitting or cutting should be
gradual, and thus exercise a less violent action on the
fibre than would obtain with an indifferent grading.
In addition to the grading of the pins, advantage
may also be taken of what is known as the “grouping,”
that is, the order in which the pins are arranged on the
tools. The grouping is of the greatest value in the
coarser-pitched tools, and although some hackling experts
prefer to have the pins in two rows on the finest
tools, the Authors consider that when all the pins in
the finer tools are in one row, the work is done better
for the line, and the tow produced is of good quality,
while such an arrangement offers the best and most
economical facilities for keeping the tools in good
condition. A good arrangement of grading and grouping
on ten tools may give a greater variation in the
splitting or cutting than would result from an indifferent
arrangement of grading and grouping on a larger
number of tools.
Three different arrangements of grading appear
below—
Number of pins per inch width of tool
¼
½
¾
1
1½
2
4
6
8
10
=
10
tools
⅛
¼
1/3
½
2/3
1
1½
2
3
4
5
6
8
10
=
14
„
⅛
1/6
¼
1/3
½
2/3
1
1½
2
3
4
5
6
7
8
10
=
16
„
All modern hackling machines should be arranged
to give the best possible yield of line, and also of tow,
from the material which is in process, since by this
effort an increase in the relative value of the finished
article is obtained, and a highly-valued product secured
at a comparatively low cost of manufacture.
As the pieces of hackled hemp are delivered from the
hackling machine, they are made up into suitably-sized
bundles and conveyed to the line store.
A record of all the materials in the various stages of
manufacture is kept in the books of the respective
departments, and such records can quickly be referred
to at any time by those who are responsible for the
production of the various classes of goods which are
being made.
As already indicated, certain classes of hemp may be
so clean when purchased, that they can be used for
some types of cordage yarns without any preliminary
hackling, and goods made in this way may compete
favourably with those made by processes which include
hackling. The object aimed at in these cases is usually
one of price and not exactly of quality, for when the
latter is the predominating condition, the superior
value is attached to the yarns made from hackled
fibre. Nevertheless, when it is simply a question of
equivalent suitability for specific purposes, and when
approximate values are obtainable by the two methods
of manufacture, the conditions offer a choice which is
of extreme importance at those times when the available
suitable fibre for either method is scarce, or when
either is very abundant.
Although the above choice presents itself for the
cases mentioned, it will be understood that for the
better grades of cordage one must employ either a very
high grade of cleaned hemp, or a grade of hemp which
has been hackled and cleaned by hand or by suitable
kinds of machines.
In very special cases, e.g., high-class threads and
cord yarns, where great strength and uniformity are
desired, it has been found advisable to prepare the fibre
entirely by a system of “hand dressing.” The hand
method lends itself naturally to more careful selective
treatment. It should, however, be stated that it is
not usual to adopt this method except for the production
of a comparatively small quantity of fine yarns,
that is, thin yarns. Sewing twines and cords should
be level and strong, but not necessarily fine, unless for
the finest class of work into which these threads are to
be introduced, as, for example, in the glove industry
in which case the fibre used is often flax. These finer
grades of threads and twines, as well as the finer classes
of cordage, may require the whole range of operations
to produce the finest and cleanest product consistent
with the work for which it is intended to be used,
although, as stated, the hand hackling may be employed
for the flax intended for use in the manufacture of fine
thin yarns, whereas, it is preferable to employ machine
hackling for the equally valuable but thicker yarns.
From this stage, however, the operations for the continuation
of the processes of manufacture from the two
distinct types of dressed line are conducted mechanically.
In perhaps the most extensive scheme of hackling
there is a combination of hand and machine work.
The first operation is termed “Roughing,” and consists
of drawing the pieces of hemp or flax through a set of
hackle pins arranged or grouped in a wooden block,
and termed a “Rougher’s Tool.” This operation,
when correctly performed, leaves the fibres practically
parallel, their ends approximately in line with each
other, and separates these long fibres from the shorter
ones which are left amongst the hackle pins, and
which are removed regularly to be ultimately used
as “tow” in what is known as the “carding” process.
These long, partially-combed and split fibres are now
taken to the hackling machine to undergo a further
treatment of combing and splitting as already briefly
described. Finally, when the pieces leave the hackling
machine they have to undergo for a second time a hand
process of hackling which is termed “Sorting and
Selecting,” after which the material is made up into a
bundle.
It is obvious that such an extensive scheme of hackling
is not only slow but also costly, and is attempted
only for the most valuable raw materials to be used for
costly finished goods such as fishing lines, fine cords,
and for valuable threads which are used in the glove,
leather and cognate industries.
It will thus be seen that there are in reality three
distinct methods of preparing the fibres into the product
known as “line,” and the finished product thus
obtained then passes through a series of machines,
termed a “system,” in which the fibres are first arranged
in such a way as to form a continuous thin and broad
ribbon termed a “sliver,” then into a more or less
circular and slightly-twisted form termed a “rove,”
and ultimately into a much finer circular and twisted
form termed a “yarn” or “single thread.” Rope and
heavy cordage yarns are often made by a simpler process
than that just enumerated. The operations which
these yarns or single threads subsequently undergo will
be discussed at the proper place. In the meantime we
purpose mentioning the different machines, and then
briefly to describe and illustrate these machines which
jointly form what we have called a “system.”
System I for Fine Classes of Line Yarn.
System II for Heavier Line Yarns.
System III for Common Yarns from Tow.
Spread Board
Spread Board
Carding Machine
Sett Frame
Sett Frame
Drawing Frames
Drawing Frame
Finishing Drawing Frame
Roving Frame
Roving and Gill Spinning
Automatic Spinning
Dry Spinning or Automatic Spinning
Dry Spinning
The machine known as the “spread-board” is so
called because the function which it performs is the
mechanical sequel to the manual operation which was
conducted somewhat as follows: A board about 9 ft.
long was covered with an even layer of the pieces of
hackled flax or hemp so arranged that each succeeding
piece partially overlapped the one immediately before
it much in the same way, so far as overlapping is concerned,
as obtains with the scales of a fish or the parts
of a fir cone. One operative would place his hands on
the material thus arranged, while another operative
would draw forward the material, reducing it in girth
but increasing it in length, by causing some of the
fibres, and all of them in turn, to slide a distance on
their neighbouring fibres. At the same time the drawn-out
material would be kept as uniform as possible in
thickness, and the operation would be continued until
the thin drawn-out length was probably five to ten
times the length of the more bulky material which was
originally laid as explained on the board.
The modern technical term for this elongation or
attenuation of groups of fibres is “drafting,” and the
dual operation described above is now performed in the
modern spread-board, the delivery end of one of which
is illustrated in Fig. 20.
Fig. 20 SPREAD BOARD
The use of the spread-board is rendered necessary
because the pieces of material from the hackling machine
are made up of individual and comparatively short
lengths of fibre, and the essential object for the satisfactory
continuation of the processes of manufacture is
to convert these short lengths into a continuous length
termed a “sliver.”
The pieces of hemp or the like are first weighed in a
balance near the feed end of the machine, and are then
arranged by hand on narrow endless travelling belts,
termed “spread leathers,” so that the thin end of one
piece of hemp is overlapped by the thick end of the
next piece and so on. These “spread leathers” form
the moving bases of narrow channels, the sides of which
keep the pieces of hemp in their own channel. But
instead of only one row of moving fibres or pieces as in
the primitive process, there may be four or six of the
above-mentioned channels.
The neatly-arranged pieces in each channel are carried
forward slowly but continuously, each group by its own
endless belt, until all the groups reach the first pair of
rollers called the back or retaining rollers. After the
pieces leave these rollers they are penetrated by a large
number of pins or hackles arranged on what are known
as “gills” or “fallers.” There may be four or six
gills on each faller, and the fallers rise in turn to cause
the pins to enter the narrow sheets of fibres, to join the
faller which immediately preceded it, and to move
along with the majority of the fallers in a body towards
the drawing rollers. In the spread-board illustrated in
Fig. 20 there are four channels, and therefore four
pressing rollers in contact with the drawing roller which
extends the full width of the machine; all the four
pressing rollers are distinctly shown near the upper
part of the illustration.
It will be understood that the four narrow sheets of
fibres will ultimately reach the drawing and pressing
rollers, and since the surface speed of these rollers is
much greater than that of the back or retaining rollers,
the fibres which are clear of the grip of the retaining
rollers will slide on those whose movements are restrained
by the rollers and gill pins, and since there is always
a quantity thus liberated, the draft is accomplished
according to the relative speeds of the two sets of
rollers. The effective contact between the rollers for
drafting is obtained by means of levers two of which
are shown near the floor and to the right of the sliver
can in Fig. 20.
The gills or fallers are moved forward by spirals or
screws and at practically the same surface speed as the
“spread leathers” and the retaining rollers; as each
faller reaches its full forward position, it is caused to
move downward and then backward in a lower plane,
and ultimately to rise again to enable the pins to enter
into a fresh portion of the sheet of fibres; after this
cycle is completed, the same functions are repeated
while the machine remains in motion.
The four slivers which leave the drawing and pressing
rollers unite into two pairs through the medium of
doubling plates; one pair of slivers thus united is
guided to a conductor, and then passes between the
delivery rollers and into a sliver can shown in the foreground
of Fig. 20, while the other pair, part only of
which appears in the illustration, follows a similar
course into a neighbouring sliver can.
The extent to which the fibres are drawn out in the
spread-board, that is, the draft of the material, varies
from about ten to twenty.
The gradual tendency to call into action mechanical
parts to perform work which was originally done by
hand is further emphasized in the latest attempt to
feed the above-mentioned short pieces of hemp or the
like automatically from the hackling machine to the
spread-board. This ingenious device, the invention of
Mr. Joshua Eves, of Belfast, carries the hackled pieces
from the holders of the hackling machine and lays them
on the “spread leather” in the channel, and, in addition,
it is provided with a regulating device to preserve as
near as possible uniformity in the thickness of the
resulting sliver which, as usual, is delivered into sliver
cans as already described.
Even with the greatest care, the most efficient type
of machine and the finest stage of hackled fibre, it is
practically impossible to achieve an absolutely uniform
sliver. In order, therefore, to approach a practicable
ideal sliver, it is usual to resort to a process of “doubling”
and a further operation of drawing; indeed, the
next machine to which the slivers pass is termed a
“drawing frame.” Before dealing with this machine,
however, it is desirable to discuss another distinct
method of forming the initial sliver from fibrous material.
In general, the sliver prepared by the spread-board
is intended for the production of level and high quality
yarns, but it is evident that, during the operations of
scutching and hackling, a certain quantity of the shorter
fibres will become detached from the main body of the
strick. These shorter fibres, termed tow, are not only
weaker than the line fibres but are also accompanied
by impurities which must be removed in the subsequent
operations; they are graded according to quality, and
ultimately treated by a distinct method which, however,
prepares them into a sliver very similar to that which
emerges from the delivery rollers of the above-described
spread-board. Then, as already mentioned, the after
processes for both types of sliver are practically identical.
The conversion of this tow into a sliver takes place
in what is known as a “carding” machine. This is a
particular construction of a general type of machine
which is used for the same purpose in most textile
trades where comparatively short fibres have to be
converted into sliver form.
The function which the card—a contraction for carding
machine—performs is to split up the fibres and to
lay them parallel with their neighbours; for this purpose
the machine is provided with a series of rollers
which are covered or clothed with sharp pointed pins,
the size, direction and inclination of which depend upon
the particular work which each set has to perform. A
set of cards comprises two or more machines each of
which differs slightly from the others, and invariably
arranged so that succeeding machines in a set are provided
with finer clothing, i.e., smaller and shorter pins
and more closely set. The simplest set is where two
machines are involved, the first one termed a “Breaker
Card,” and the second one termed a “Finisher Card.”
In both machines a series of comparatively small rollers,
say from 8 to 20 in. diameter, and covered with pins,
are arranged partially round and close to a large central
roller of 4 to 5 ft. diameter, also covered with pins and
termed a cylinder. The general appearance of the
machines will be gathered from the two rows in Fig. 21;
the nearest machine on the left shows the delivery
side of a breaker card where the sliver is delivered
into a can; the nearest machine on the right illustrates
both feed and delivery sides of a finisher card.
Fig. 21 BREAKER AND FINISHER CARDS
The tow, which has been previously softened, is laid
as evenly as possible on a travelling endless sheet by
means of which the fibrous material is carried to the
pins of the “feed roller” which rotates very slowly
and at the same surface speed as the feed sheet. Immediately
the material emerges from the feed rollers,
or feed roller and “shell,” it is acted upon by a series
of hackle pins projecting from the periphery of the
cylinder, and moving at a surface speed of more than
2,000 ft. per minute. The fibres are therefore combed
and carried off the pins of the feed roller by the pins
of the cylinder to a series of rollers arranged in pairs,
each pair consisting of a “worker” and a “stripper.”
When the fibres on the pins of the cylinder reach the
first pair of worker and stripper, the bulk of the material
is carded and ultimately returned to the pins of the
cylinder to be carried to the next pair of rollers, and so
on, until it has been sufficiently equalized and cleaned
for the particular yarn into which it is to be made.
By this time the uneven fibres have been considerably
reduced in thickness, and have indeed been converted
into a thin wide film or sheet of fibrous material, and
in this state it is removed from the pins of the cylinder
by the pins of a “doffing roller” or “doffer.” The
thin, broad film of fibres now enters between a pair of
drawing rollers—seen near the top of the machine on
the left in Fig. 21—and into the upper and wide part
of an almost vertical tin conductor. The width of this
conductor decreases from the upper to the lower end,
and ultimately its width is contracted to about 3 in.
where the contracted sheet, now much thicker and about
3 in. wide, is in the well-known form of a sliver. The
sliver emerges from the mouth of the conductor, enters
between the delivery rollers and ultimately drops into
a sliver can in a very similar manner to that depicted
in Fig. 20.
About ten or twelve of these sliver cans from the
breaker card are now transferred across the space,
termed a “pass,” to the feed of the finisher card on the
right of Fig. 21. These ten or twelve slivers are fed
into this machine and they undergo a further and
similar treatment with from four to six pairs of rollers,
and finally the finished and single sliver is delivered
into a can near the side of the machine. In
both machines the material is drafted according to
requirements.[1]
We have thus arrived by two several ways at the
production of a continuous sliver. Both types of sliver
pass next to what is known as a “Drawing Frame,”
or rather to a set of drawing frames, usually termed,
first drawing, second drawing, third drawing, and so on,
if more than three are employed.
The machines used for the two kinds of slivers are
practically identical in principle and construction, the
only difference being that provision is made to suit
the lengths of fibres of which the respective slivers are
formed; in technical phraseology the “reach” for the
line sliver is longer than the “reach” for the tow
sliver and is, approximately, proportional to the maximum
length of fibres which compose the two types of
sliver.
It will be understood that, in general, the ultimate
aim is the production of a thread of some kind, the
sectional area of which is less than that of the sliver
which is produced either at the spread-board or the
finisher card. And it will be obvious that if we unite
two or more slivers at the feed side of the “Drawing
Frame” we increase the thickness or volume proportionately;
hence, if the sliver which is delivered from
the drawing frame is required to be smaller in volume
than any of the single slivers which enter the machine,
and this is generally the case, although not universally
so, the process of drawing out the fibres, or drafting,
must be continued. In the first drawing frame uniformity
is chiefly the object, and it may happen that
in the combined processes of doubling and drafting it
may be convenient to produce in this frame a sliver
of greater volume than the individual slivers at the
feed. In such cases, most of the drafting would take
place in the succeeding drawing frames.
The first drawing frame is often termed a “Sett
Frame,” and sometimes a “Doubling Frame.” The
first-named of the three owes its designation to the
process of attenuation or drafting, the second to the
number of slivers which in the process are employed to
form one sliver, and the third to the particular case
where two slivers only are united. Although the exact
meaning of doubling is the combination of two slivers,
the same word is used however many slivers are combined
in one group.
The drawing frame has a great resemblance to the
spread-board, so far as the principles of the operations
are concerned; it differs from it in the fact that whereas
the latter is fed by short detached lengths, the former
is fed by continuous slivers.
The length of sliver which is delivered from the
spread-board is measured; this is accomplished by the
size of one of the drawing rollers and the necessary
subsequent mechanism; these jointly cause a bell to
ring, or to move a hand over the face of a clock. The
length thus indicated is called the “bell or clock length,”
and whichever system is adopted, the operative receives
a certain weight of material which must be fed into the
machine between two consecutive ringings of the bell,
or during the time that the clock hand makes one
complete revolution.
The cans are weighed as they are filled and the net
weight of the sliver marked on. After a sufficient
number of cans have been filled, say eight, averaging
20 lb. each, or 160 lb. in all, and the length of sliver
in each can, say 250 yd., eight cans are placed at the
feed side of the drawing frame. The average weight
of the combined slivers on entering the drawing frame
is, therefore—
160 lb. × 16 oz. per lb.
= approximately 10 oz. per yd.
250 yd. length
If the draft is, say 12, the 160 lb. of material when
delivered in the form of a single sliver will be—
250 yards × 12 draft = 3,000 yd.
Then—
160 lb. × 16 oz. per lb.
= 0·85 of an ounce per yd.
3,000 yd. of sliver
The operation of drawing is conducted as in the
spread-board by means of retaining or back rollers,
gills, drawing and pressing rollers. It should be again
pointed out that the distance between the retaining
rollers and the drawing rollers—termed the “reach”—should
be regulated by the length of the fibres under
treatment, and should be greater than the longest
individual fibres, otherwise such fibres, instead of sliding
on those already held, would obviously be broken
because the surface speed of the drawing rollers is much
greater than that of the retaining rollers; in the case
under notice the ratio is 12 to 1.
The best scheme yet devised for filling up this intervening
space between the two pairs of rollers, and of
providing support for the moving fibres is that of the
above-mentioned gills. The use of gills in the machine
is of great importance, for on the correct adaptation of
the gills to the material in process depends the degree
of efficiency of the machine.
As the gills move from the retaining rollers towards
the drawing rollers in virtue of the action of suitable
spiral or other mechanism, each group forms a compact
sheet or field of hackle pins, and this field of pins regulates
and restrains the movements of the fibres to the
requisite extent as the latter move amongst them due
to the pulling action of the drawing rollers.
In this way each individual sliver in its own set of
pins is reduced in size, and any local defect in a sliver
is calculated to be overshadowed or eliminated when
the said sliver joins the remainder of the slivers at the
“doubling plates” which are situated between the
drawing and the delivery rollers. The result is, therefore,
a single sliver of greater uniformity than any of
the constituent slivers, such sliver being smaller, equal
to, or greater than, any of the individual slivers from
which it has been made according to the ratio of the
doublings and draft.
A series of drawing frames in system as illustrated
in Fig. 22, will provide the necessary doubling and
drafting, and so reduce the sliver to a suitable size for
use in any of the following yarn-forming or spinning
machines—
(a) The Roving Frame which would be used to convert
the sliver into a somewhat circular form, and
simultaneously to wind this twisted sliver on to a large
two-ended bobbin ready for the spinning frame (dry
spinning).
(b) The Gill Spinning Frame which is a machine by
means of which very high-class yarns can be produced
with a perfect system of drafting and twisting in one
operation.
(c) The Automatic Spinning Frame in which the
heaviest class of cordage yarn is spun by the simplest
and most direct method.
Fig. 22 DRAWING FRAMES
The roving frame is one of the most complicated
groups of mechanism and one of the most perfect
machines which is used in the whole system. Its
function is of a multiple type, for the mechanism of
the machine not only necessitates the use of retaining
rollers, gills and drawing rollers to effect a draft, but
after the reduced sliver has been passed through the
delivery rollers, it introduces a certain amount of twist
to the sliver—incidentally making it somewhat circular
in section—and finally winds the twisted sliver, termed
“rove,” on to a large bobbin.
The method of drafting has already been briefly
described, hence, no recapitulation is necessary. The
essential amount of twist for each individual sliver is
imparted by its own spindle, an upright rod which
rotates rapidly, and upon which the large bobbin runs
or rotates loosely, while attached to the top of the
spindle is a “flyer” resembling an elongated inverted
U, thus: . Most of these parts are clearly seen in
Fig. 23, which represents, of course, the delivery side
of the machine. At the other side of the machine,
the feed side, there is a sliver can with its sliver for
each thread and bobbin, the bobbins being arranged
in two rows upon discs in corresponding holes in the
long shelf, termed the “lifting rail,” the “builder rail,”
or simply the “builder.”
Fig. 23 ROVING FRAME
The extreme ends of the two legs of the flyer are
bent to form or carry eyes, and into one of these eyes the
twisted sliver is passed, while between this eye and the
delivery rollers the sliver is centralized by passing it
through a guide eye. The function of the eye in the flyer
is that of guiding or winding the rove on to the bobbin,
and this is made possible because the bobbin itself is
made to rise and fall between the legs of the flyer through
a distance equal to the length of the bobbin—hence the
necessity for the long legs of the flyer or inverted U.
The spindles and bobbins are driven independently
and positively by wheel gearing, and it is obvious that
the rove must be wound on to the bobbin at the same
rate as it is produced. Since the speed of the drawing
and delivery rollers is constant, the delivery of the
sliver is constant, and so is the production of rove,
although the length of rove delivered is infinitesimally
less than that of the sliver in virtue of the small contraction
which takes place during the twisting. If the
diameter of the rove on the bobbin always remained
the same size, which is obviously impossible, the revolutions
of the bobbin would be constant. But every
layer of rove which is wound on to the bobbin by the
joint action of the rotating spindle, the rotating bobbin,
and the vertical movement of the bobbin on the builder,
adds for each vertical movement, up or down, one more
layer of rove to the partially-filled or empty bobbin,
and thus increases the diameter of the combined bobbin
and rove. Hence it is necessary to impart what may
be termed an intermittent and variable motion to the
bobbin; this is done by an exceptionally unique and
intricate group of mechanical parts termed the “differential
motion.” The function of the differential
motion is to alter the speed of the bobbin after each
complete layer of rove has been wound on to it, because
it will be clear that when the direction of the builder
is changed, the winding of the rove is performed on a
diameter which is greater than the last by approximately
twice the diameter of the rove. The discs
upon which the bobbins rest are provided with two
vertical pins which enter two of the holes in the flange
of the bobbin, seen clearly in the empty bobbins near
the frame, and by means of which the bobbins are
driven at the desired speed. Accurate adjustment of
the parts is necessary, and a lengthy description with
numerous line drawings are essential to a clear understanding
of this ingenious mechanism.[2]
Spinning.—The bobbins filled with rove yarn, as
illustrated in Fig. 23, are ready to be removed or
“doffed,” as the operation is technically called, preparatory
to being taken to some type of spinning frame
where a further extension or “draft” of the yarn takes
place, and simultaneously the finished product of the
desired thickness or “count” is wound upon a much
smaller two-ended bobbin.
A large-used type of dry spinning frame is illustrated
in Fig. 24, and this type of machine is usually employed
for spinning yarns the “counts” or “sizes” of which
are represented by the numerals 3 to 16. Yarns which
happen to be of lower or higher count than these limits
are produced on other similar or different type of
machine.
In Fig. 24 the large rove bobbins are seen distinctly
on projecting pins—termed a creel—at the top of the
machine. Each rove from its bobbin, which can rotate
freely on its peg, is passed between retaining rollers,
and over what is known as a “breast-plate,” through
the contracted groove of a “tin conductor,” between
a pair of drawing rollers, through a slot in the
“thread-plate,” through an eye in one of the legs of the
flyer, and ultimately on to the bobbin which rotates on a
spindle upon the upper end of which the flyer is fixed.
In “long-reach” machines it may be necessary to use
additional rods or binders which act as auxiliary
breast-plates.
By permission of the Edinburgh Roperie Co. Fig. 24 DRY SPINNING FRAME
All the spindles on one side of the frame are individually
driven by flat tapes or round bands from a
driving tin cylinder situated near the floor and inside
the frame as shown in Fig. 24, and driven direct from
the main pulley. The flat tape or band passes partially
round this cylinder, and then partially around a “whorl”
or bobbin-shaped pulley of about 1½ to 3 in. diameter
on the spindle; these whorls and tapes are seen clearly
on the first three spindles in the illustration, and in the
same line as the “temper weights.” The latter hang
from cords attached to the back of the “builder”
which imparts the up and down motion to the bobbins
during the operation of spinning, and so enables the
yarns to be distributed over the full length of the bobbin.
The cord which is attached to the temper weight is
caused to bear on the grooved flange of the bobbin,
and by moving the cord into successive grooves or
notches in front of the builder as the bobbin fills, a
greater part of the groove is acted upon by the cord
and weight, and thus the drag is increased.
Demi-sec spinning, as the name implies, refers to a
process between dry spinning and wet spinning. In
the demi-sec frames a slight quantity of water is added
to the drawn-out and partially-twisted threads as the
latter pass from the drawing rollers to the flyers. The
purpose of this moisture is to smooth and lay the hairs
of fibre which would otherwise project from the main
body of the yarn as in the case of dry-spun yarns. It
is usual to apply this method of spinning to thread
yarns.
The draft necessary for converting the rove to the
desired size or count of yarn is regulated by changing
the value of the gearing, the wheels of which are enclosed
in the oval covering at the end of the view in
Fig. 24; near this covering is also seen the heart-shaped
cam, lever and rod which are used for operating the
builder.
Gill Spinning.—In the ordinary spinning frame the
material supplied is from rove bobbins, but in the gill
spinning machine, the material is supplied as a sliver
from a sliver can, one for each spindle. The gill spinner
has a drawing head similar to that in a roving frame,
and the spindles and flyers are usually driven by bands.
The machine used for gill spinning might be compared
with a roving frame with or without the winding motion
or differential gear.
[1] For an exhaustive description of Carding see the Authors’
work on Jute and Jute Spinning: Part I.
[2] Readers who are sufficiently interested in this and several
other machines which are briefly described in this work, might
consult the following works of the Authors, which are at present
appearing serially, and which will be published in book form
when completed: “Jute and Jute Spinning”: The Textile
Manufacturer; “Flax and Flax Spinning”: The Textile Recorder.
CHAPTER VIII THE PREPARING AND SPINNING MACHINERY FOR MANILA AND OTHER HARD FIBRES
The method of producing yarns from the hard fibres
involves the use of quite different machines in the preparatory
processes; this departure is necessary on
account of the nature of the material and the length
of the raw fibre.
The bales of raw material, Manila, Sisal, New Zealand,
or the like, but all from one type in general, are
arranged in a convenient position near the feed of the
first machine which is called a “Hackler and Spreader,”
and one type of which is illustrated in Fig. 25. The
bales which are grouped together for this first treatment
are chosen from different “marks” or grades of
fibre in order to mix them to secure uniformity and
to produce yarns of a given quality at the desired
price.
Fig. 25 HACKLER AND SPREADER
The heads of material are split up into suitable and
uniform stricks, and when various classes are to be
mixed it is essential that proportionate quantities should
be drawn from the various bales in the “batch” or
blend, and fed proportionately and uniformly on to the
feed sheet of the machine. The feed sheet conveys the
stricks slowly towards and ultimately between a pair
of retaining and feed rollers, and when the material
emerges from these rollers it is acted upon by a series
of large hackle pins fixed in a chain of fallers or bars.
These pins move at twice the speed of the feed and
retaining rollers, and this relative movement enables
the pins to hackle and open out the stricks. The
partially-hackled stricks are now conveyed to a second
chain of fallers and hackles which move at a much
greater speed than that of the first hackles; it is here
where most of the drawing takes place, and the material
as it leaves these hackles is in the form of a thin sheet
of fibres which enters a pair of drawing rollers. Finally,
the material is delivered on to the floor in the form of
a sliver and at the opposite end of the machine.
The bundles of sliver are conveyed to another machine,
termed the intermediate machine, where further processes
of equalization and drawing take place. In this,
and in any subsequent machine of the same type, of
which there may be three or four, the slivers are fed
as illustrated on the left of Fig. 26, while several lengths
of slivers appear in the foreground. After the drawing
and hackling operations, the sliver is delivered as
illustrated. These processes prepare suitable slivers
for the remainder of the operations which are somewhat
similar to those which are used for the soft fibres,
although the “reach” in the machines for the hard
fibres is very much longer than that necessary for the
soft fibres. In the final preparing machine, the sliver
is delivered into sliver cans which are then taken to the
automatic spinning frame.
Fig. 26 INTERMEDIATE MACHINE
Automatic Spinning Machines.—A row of automatic
spinning machines is illustrated in Fig. 27. The slivers
from the last drawing frame are placed at the feed,
one sliver can with its length of sliver for each machine.
The sliver is passed through the first conductor, situated
about a yard above the sliver can, and then between a
pair of feed rollers seen to the right of the machine.
From here the sliver is deflected to the proper bell-mouth
conductor and to the long stretch or reach of
gill pins shown clearly in the view. On emerging from
the gill pins, the sliver passes through a nipping die
and thence to the enclosed flyer from which it is wound
on to the bobbin.
Fig. 27 AUTOMATIC SPINNING MACHINE
The drafting is accomplished by a series of rollers or
pulleys which draw the fibres through the gill pins and
the nipping die, while the twist is imparted as usual
by the flyers which revolve at about 1,400 revolutions
per minute. The flyers are now enclosed in a safety
cage of about the same width as the name plate.
The yarns thus spun are built upon large steel-ended
bobbins which, when filled, may be conveyed direct to
the transferring or warping machines where the yarns
are prepared for further treatment, if and when any
further treatment is necessary, or to the rope machines.
Thus, if the yarns are to be made up into a tarred
rope, it is necessary to prepare them into a suitable
form for the tarring operation. This usually takes the
form of a warp, and such warps are most satisfactorily
made on a warping mill or winding reel. It is usual
to run twelve threads from twelve bobbins and to make
the warp a suitable size by continuing the operation of
warping in the same way as is done for warps which
are to be woven in a loom.
The warp is then passed through a tarring machine
in which the tar, usually Russian or Swedish, is kept
warm during the operation. After the necessary amount
of tar has been applied, it is usual to store the warps
of yarn for a lengthened period, say up to six months,
to condition them. The individual yarns from these
warps are then rewound on to twelve large bobbins in
what is known as a 12-bobbin vertical spindle-winding
machine.
CHAPTER IX TWINES, CORDS AND LINES
There are many instances in which yarns made by the
foregoing operations are incorporated in twines, cords
and ropes, while, on the other hand, special types of
machinery are utilized to manufacture certain grades
of such goods with an entirely different system of
machinery. It is in connection with the latter branch
that this chapter will for the most part treat, but,
before dealing with these machines for specific purposes,
we might just say that there are huge quantities of
yarn spun by the methods already described, and the
single yarn so spun is then twisted so that the resulting
compound may contain two single threads twisted
together, or any other greater number twisted either
in one operation, or two or more separate operations,
to obtain the desired type of cordage. In many cases
the yarns have to be bleached before they are twisted,
and Fig. 28 illustrates the drying of bleached yarns.
Fig. 28 DRYING BLEACHED YARNS
The terms twine, cord and rope all indicate to the
textile technologist a multiple structure, that is, an
article in which two or more single threads are united
by the process known as doubling, folding or twisting.
Thus, in the manufacture of twines, of which there
is a great variety, the process is a comparatively simple
one. A number of bobbins are arranged on pins in a
creel somewhat similarly to those illustrated in the
spinning frame in Fig. 24. The requisite yarns, from
2, 3, 4 ... n bobbins, for the type of twine in process
are led from the bobbins through an eye or guide
or through a “register plate,” then between a pair of
drawing rollers, and thence to the flyer and spindle as
in the spinning operation. As the spindle and flyer
rotate, the group of single yarns are drawn through the
guide or eye, or through the register plate by the drawing
rollers, and the necessary amount of twist applied
before the finished product is wound on to the bobbin.
The amount of twist, or the technical term “twist
per inch,” is fixed by the speed of the spindle and the
delivery of the yarn by the drawing rollers. In other
words we have—
revs. per min. of spindle
=
the number of turns per
delivery of twine in in. per min.
in. or the twist per in.
There is this difference between spinning and doubling
or twisting; when a thread breaks in spinning, the
supply of yarn to the bobbin ceases, and the production
from that spindle stops until the broken thread is
repaired; on the other hand, when two or more threads
are being twisted together and wound on to a bobbin,
it is evident that if one thread breaks the supply is not
stopped entirely, but the product is defective because
it is short of that yarn. In order to prevent the production
of faulty goods and to minimize waste, it is a
common practice to introduce delicate mechanical parts
to such frames, the function of which parts is to stop
the delivery of yarn to any spindle in connection with
which any of the constituent threads are broken. A
frame so fitted is said to have an “Automatic Thread
Stop Motion.”
In many cases the twines made by the above process
are taken to another machine in which a number of
bobbins are again arranged on pins, the twines passed
under rollers and immersed in polishing mixtures of
starch or size contained in troughs or boxes. A quantity
of the size adheres to the twines as they pass through
it, and revolving brushes are used to remove the excess
of size and to clean the twines. These operations are
repeated a few times and ultimately the twines so
starched, cleaned and polished are led over drying
cylinders in front of which are placed rollers covered
with suitable material, usually coir yarns. These rollers
rotate at a high speed, and sometimes wax is applied
to the coir yarn-covered rollers, so that the twines are
dried, polished and finished simultaneously before they
leave the hot cylinders to be wound on to a second set
of empty bobbins. This machine is usually termed a
“bobbin to bobbin polishing machine,” and the bobbins
upon which the twine is finally wound are frictionally
driven because the delivery of twine is constant. In
this way the requisite finish or polish is applied to the
surface of the twine, and this gives the twine the smart
appearance which makes it quite attractive.
In the operation of twisting single yarns, that is, in
the roving frame and in the spinning frame, it is usual
to impart what is known as a “right twist.” Thus,
if one looks down on a spinning or roving spindle and
the direction of rotation is clockwise, then the twist
imparted is right hand. On the other hand, if, when
viewed from the same position, the spindle rotates
counter-clockwise, the definition is “reverse” or left-hand
twist. When two single threads of right-hand twist
are combined in twisting as in the formation of the
above-mentioned twines, it is usual for the doubling
or twisting spindles to rotate counter-clockwise. This
is done for practical reasons which need not be discussed
here, but, although this is the usual way, there are
cases in the twisting of textile threads where two right-hand
twists are combined with the same direction of
twist. Some such definition as the above will help
considerably to elucidate the structure of more
complicated multiple-twist cords.
Cords.—In the manufacture of cords, three or more
twines are combined. Thus, if three twines, each of
reverse or left-hand twist and made from two single
yarns of right-hand twist, are combined together by a
further process of twisting, it is usual to apply a right-hand
twist to these three two-ply twines. When treated
in this way, the finished article is termed a cord which
is “cable laid.” And, in general, in the twisting of
such cords, each successive twisting operation is in the
opposite direction to that which immediately preceded
it.
Whip-cords, fishing lines and window-blind cords are
typical of this structure which, in general, involves the
use of complicated machinery or else a long rope walk.
The single yarns are first made into twines and finished
as already described; afterwards the necessary number
of twines to form the cable-laid cord are united.
The operation is a costly one when compared with
the simpler process of twine making, but the cable-laid
cord is a much more handsome product than the twine,
and is admirably adapted for purposes where a smart
compact and ornamental structure is desired or necessary.
Box Cord.—Box cord is a very simple form of cordage,
the method of manufacture being quite different from
that of the foregoing laid cords. In the box-cord process
there are two distinct groups of twisting operations
conducted simultaneously. The single threads, of which
there may be from two to eight, receive the necessary
additional twist by a corresponding number of flyers
which differ in shape, however, from the ones in roving
and ordinary spinning in that they are known as enclosed
flyers. While these individual threads are being
twisted, the several yarns converge towards, and pass
direct to, the eye of another enclosed flyer which completes
the process by twisting the component threads
in the opposite direction to that imparted to the single
threads by the two to eight different flyers. It should
be mentioned that the building of the completed box-cord
on the bobbin is accomplished by suitable
mechanism attached to the flyer.
The machine is comparatively simple, and the attendants
need little experience beyond that of detecting
broken threads and repairing them. It need hardly
be pointed out that the omission of a thread from the
requisite number in the group for the finished cord is a
fault the prevention of which constitutes one of the
chief duties of the attendant. The finished product is
termed two-ply, three-ply, ... eight-ply box-cord
according to the number of single yarns which are
utilized. Practically all classes of fibre are used in the
manufacture of these goods, and this method of twisting
is largely adopted for the making up of comparatively
light cords from fairly heavy sizes of yarn. The product
is used extensively for tying boxes and large
packages and thus serves the purpose of a light rope
which is a more expensive article.
Plaiting or Braiding.—Special classes of lines and
cords are now made on a machine of an ingenious design.
One of the advantages of this machine is the fact that
great lengths of line can be made; indeed, there is
practically no limit to the length which may be made
beyond that of the difficulty of handling the huge size
of the finished product.
The machine, which is complicated and costly in its
upkeep, is used extensively for the production of log
lines, sash cords, and a large variety of blind cords.
The requisite number of threads for the cord are wound
on a suitable number of bobbins, and the latter are
placed in carriers in the machine. The yarns or twines
are passed over or across each other in such a way
that they are locked in position and in the well-known
plaited form which is characteristic of this class of goods.
This scheme of interlocking is formed by an even number
of groups of threads, usually eight or more, and the
movements of these groups, or rather the bobbins which
contain them, are practically identical with the familiar
“grand-chain” in circle dances practised by children
and also by grown-up persons. Alternate bobbins move
sinuously round a circle in one direction, while the
remaining alternate bobbins move similarly in the
opposite direction. Each bobbin passes those in the
other group first on the left and then on the right of a
circle whose path is the centre of the two sinuous paths
described by the two sets of bobbins.
The continuous movements of the two sets of
bobbins in each machine form the elegant cord which,
when plaited, passes through a guide eye in the centre
of the circle but in a higher plane. From this eye the
cord rises to a pair of hauling-winch pulleys around
which it passes a few times forming the figure 8.
Finally, the cord passes between a pair of delivery
rollers into a large box at the back of the machine.
The hauling-winch pulleys and the drawing rollers,
which combined give the necessary firmness, are driven
positively and accurately so that their surface speeds
may coincide with the amount of cord which is formed
at the guide eye.
CHAPTER X ROPES AND ROPE MAKING; YARN NUMBERING
A considerable quantity of the smaller-sized ropes are
now made on what are termed “house machines.”
These machines perform the same function as those in
the rope-walk but they occupy a much smaller space;
they are adapted to deal with a great range of sizes
although, in general, it is not necessary to use one
machine for a large range of work; there is such a
variety of ropes in use that in a well-equipped rope
works it is possible to keep each machine almost constantly
on ropes within a small range of size. These
remarks refer, as indicated, to ropes which come within
the limit of, say 2 to 3 in. in circumference. In the
manufacture of the larger sizes of ropes, it is usual to
use two distinct machines, one termed the “strander,”
and the other the “closer,” and, although the house-machine
made ropes are often considered inferior to
those made in the rope-walk, many of the objections
urged against the untarred ropes made in the house-machine
are more imaginary than real.
Fig. 29 is illustrative of a number of machines of a
type used for the making of ropes in which twelve to
forty-five threads may be combined in one operation
during the manufacture of a three-strand or a four-strand
rope. The bobbins are placed in creel flyers of
which there may be three or four according as the rope
is to be a three-strand or a four-strand one. The creel
flyers are composed of two parts, one of which carries
the bobbins, and the other carries the hauling and
twisting gear. All the three or the four strands are
made at the same time; when formed, they leave their
respective flyers and converge towards the top and the
die or central tube where they are formed into a rope
by the proper degree of twist according to the purpose
for which the rope is to be used. Finally, the finished
rope is drawn forward by a series of hauling pulleys
which also conduct the rope to the winding-on reel or
bobbin, and by suitable mechanism the rope is wound
into a temporary form of coil. As the bobbins are
filled with rope they are removed from the machine
and conveyed to special coiling machines where they
are measured when necessary as they are made up into
coils suitable for the particular purposes desired. A
common length of coil is 120 fathoms.
By permission of the Edinburgh Roperie Co. Fig. 29 ROPE-MAKING (HOUSE MACHINES)
Although the various house machines represent the
latest developments in the art of stranding and closing—the
two essential operations of rope making—a modern
rope and cordage works is provided not only with the
various machines which have been illustrated and described,
but also with a well-equipped rope-walk so that
the products may include a great variety of cordage
from the finest lines to the mammoth ropes for ships,
steamers, harbours and heavy hauling purposes generally.
The combination of the house machines and the
modern rope-walk makes present arrangements very
complete when compared with the old type of rope-walk,
but the apparatus employed in these old rope-walk
machines embodies all the principles of construction
which are present in the new machines for the same
class of work.
Rope-walks are, naturally, long, narrow buildings
because the full length of the rope is in one stretch.
The work which is conducted in such places and the
type of building is admirably portrayed in the first
three verses of Longfellow’s poem—
THE ROPE-WALK.
In that building long and low,
With its windows all a row,
Like the port-holes of a hulk,
Human spiders spin and spin,
Backward down their threads so thin,
Dropping, each, a hempen bulk.
At the end an open door;
Squares of sunshine on the floor
Light the long and dusky lane;
And the whirling of the wheel,
Dull and drowsy, makes me feel
All its spokes are in my brain.
As the spinners to the end
Downward go and re-ascend,
Gleam the long threads in the sun;
While within this brain of mine
Cobwebs brighter and more fine
By the busy wheel are spun.
At the top of the rope-walk is a stand or bank which
contains the bobbins of yarn, and this yarn may be
dry or tarred according to requirements. The bobbins
are arranged on pins and the necessary number of yarns
for each strand are drawn from the bobbins and passed,
in their proper order for ensuring a uniform strand,
through a number of holes in a “register plate” immediately
behind the machine. In a modern machine any
number of strands up to six can be formed at the same
time, and hence there will be six register plates for the
yarns. For the larger-sized ropes only one strand can
be drawn out in one operation.
A machine termed a “traveller,” is employed to
draw out the strands, and this machine is provided
with a series of hooks as well as a central spindle.
The strands may be attached as required either to
the hooks or to the spindle. A rope-driving gear causes
this traveller to move on rails down the walk and
for the distance required, and it will be evident that
as the traveller recedes from the bank it will draw
the groups of threads from the bobbins and through
the register plates; at the same time the several hooks
are caused to rotate, and thus each strand is twisted
and hauled simultaneously.
When the traveller has moved backwards or downwards
for the necessary distance to form the length of
strand, the strands are removed from the hooks and
attached to suitable supports until a sufficient number
has been made for closing or laying-up.
To form the strands into a rope, it is essential to use
a fixed or stationary machine along with the traveller and
a top-cart. The stationary machine is substantially built,
and, inter alia, is provided with a central spindle around
which are grouped a set of hooks—usually in sections
of two circles. Two wheels on the central spindle
drive a number of pinions, one behind each hook, the
ratio of one wheel to half the pinions is 34 to 16, while
the ratio of the other wheel to the other half of the
pinions is 54 to 11. Thus, the revolutions may be—
1
to
1
when the strand is on the central spindle,
34
to
16
or
approx.
2 to 1 when on large hooks, and
54
to
11
„
„
5 to 1 when on small hooks.
When the necessary strands to form the rope are
stretched between the stationary machine and the
traveller, an extra amount of twist is imparted to each
strand, an operation which is termed “hardening the
strand”; the amount of twist can be judged only by
past experience, although it is common to give instructions
in the words “harden so many fathoms”; at
other times the strands are hardened until the threads
form a desired angle. In all cases the strands should
be twisted equally so that the same tensile stress is on
each strand. After this twist has been applied, all the
strands are placed either on one of the hooks or on the
central spindle of the traveller. A top-shaped block is
put into position inside the three strands—this top is
in full view in Fig. 30, which, by the way, illustrates
the laying of a 28-in. circumference four-strand hawser
with a central core—and the machines started for a
few revolutions. When the first make of the rope is
formed, the top is brought back to its proper place, a
few pieces of rope, termed tails, are placed round the
newly-formed portion of the rope, and these may be
collected and held in position by a bar as shown; one
of these tails was removed when the photograph was
taken in order to show the finished part of the rope
between the top-cart and the traveller. The traveller
is now braked to keep the rope taut while the rope-maker
lays the strands, the hooks of the stationary
machine at the top of the walk as well as the hooks on
the traveller being rotated meanwhile at a speed which
is suitable for the make or lay of the rope. The hooks in
the two machines rotate relatively about 7 to 9 or 7 to 11.
Fig. 30 LAYING OF A FOUR-STRAND CABLE-LAID ROPE IN THE ROPE-WALK
When a hawser or cable-laid rope or a “trawl warp”
is desired, the formed ropes are again placed in position,
and the whole routine repeated, while if the warp is to
consist of more than three strands, a heart must be
inserted, as exemplified in Fig. 30, upon which to lay
or build the strands. It will be understood that the
view in Fig. 30 is the interior of “a rope-walk,” and that
the operative is looking towards the top of the walk
where the stationary machine is situated.
After the laying is completed, the finished rope must
be made into a coil ready for transportation. The
coiling machines are often in close proximity to the
house machine or the rope-walk, and for the coiling
of such ropes as that illustrated in Fig. 30, it is obvious
that the machine must be of substantial build. When
such a large rope is complete and ready for despatch,
it resembles the 18-in. circumference mooring rope in
Fig. 31; this rope was 90 fathoms long and two tons
weight, and was coiled in about ten minutes by a
machine specially designed for the purpose.
Fig. 31 VIEWS OF LARGE AND MEDIUM-SIZED COILS OF ROPE
Rope driving has practically revolutionized the construction
of modern mills since ropes are used not only
as a direct drive from the rope pulley on the engine or
motor shaft, but at many intermediate places, and have
replaced many installations of wheel-gearing. These
mill-driving ropes, which are invariably from 1½ to 2 in.
in diameter, are made extensively of cotton, hemp or
manila. In exceptional cases more than forty such ropes
are used on the same pulley. The frontispiece illustrates
a rope drive in which seven ropes each of 1¾ in. diameter,
are utilized on the shaft of a motor for conveying the
motion to a mill shaft seen in the distance. Other
ropes are seen in the next rope alley. Somewhat
similar ropes, but of a smaller diameter, are used for
hauling in the baling press illustrated in Fig. 15.
There are several methods of numbering yarns, most
of which involve a direct relation between the weight and
length. Thus, to quote six of the most widely-practised
methods in the textile industry we have
Silk:
count no.
=
the no. of
hanks
of
840
yards
each
in
1
lb.
Cotton:
„
=
„
hanks
„
840
„
„
„
1
„
Wool:
„
=
„
skeins
„
256
„
„
„
1
„
Worsted:
„
=
„
hanks
„
560
„
„
„
1
„
Linen:
„
=
„
leas
„
300
„
„
„
1
„
Jute:
„
=
the weight in lbs. of 14,400 yards
Hemp is sometimes reckoned according to the linen
system and sometimes by the jute system.
An entirely different method of counting or numbering
obtains in regard to ropes. The system of yarn
numbering for ropes depends upon the number of single
yarns or threads required to make one strand of a 3-in.
3-strand rope. Thus, if 25 yarns are required to
form such a strand, the yarn is 25’s, while if 30 yarns
were required for the same thickness of strand, the
yarn would be 30’s, and so on. The tube through
which the yarns are drawn is nearly half an inch bore.
If the yarn number is multiplied by 5, the product
represents the number of yards of yarn in 1 lb. Thus,
in the above 25’s yarn there are
25’s × 5 = 125 yd., or 375 ft. per lb.
Ropes are usually designated by their circumferences
in inches, and also by the number of strands neglecting
the heart if such is required.
CHAPTER XI MARKETING
It is essential in modern times that goods which are
placed on the market should be as attractive as it is
possible to make them, and cordage forms no exception
to this rule. The acme of attraction may be said to
have been reached when a sale is effected more from
appearance than from any immediate want, and this
is the ideal to be aimed at. No detail which will make
the goods attractive or memorable should be omitted.
Carelessly made-up goods are quickly noticed, and however
high may be the quality of the article, an indifferent
make-up creates an unfavourable impression which is
difficult to remove.
Little things, insignificant in themselves, often form
the nucleus of great undertakings. Mnemonic titles,
trade names, distinctive labels and the like are all
adopted to safeguard the interests of the maker, to
guarantee his products, to spread his fame, and to keep
his goods constantly in the mind’s eye of the purchaser.
Whilst no great effort is necessary to parcel up small
articles in an attractive form, it seems hardly possible
to deal with bulky articles with the same degree of
success. Nevertheless, several of these heavy and unhandy
articles are elegantly made up as is emphasized
by the coils in Fig. 31. This is the usual way of making
up ropes, and the size of the coil depends partly upon
the length of the rope, partly upon the use to which
it is to be put, and partly upon the thickness. If the
ropes are to be cut up into definite lengths, the coil
will be a multiple of that length; if otherwise, a common
length of rope is 120 fathoms as already stated.
The smaller coils, and the better grades of larger
coils, are often enclosed in paper, while the larger ones
are covered with wrappers of suitable texture to ensure
the arrival of the ropes in good condition at their
destination. The coils themselves are securely bound
as exemplified in Fig. 31 to prevent the displacement
of the structure during transit or handling, and, in
addition, many of these large and valuable ropes are
entirely covered by a cheap rope binding.
A large quantity of ropes, cords and twines are made
into hanks or “rands,” as they are termed, on a special
machine. For short lengths this method of making up
is very compact, very neat and very convenient for
marketing.
Binder twine is first made up into standard size balls
which must fit the boxes on the reaping and binding
machines; afterwards they are packed in bales ready
for despatch.
Other varieties of twine are made up in the same shape
of balls as above, but the sizes of the balls depend upon
many circumstances. Large quantities for the retail
trade are made up into convenient sizes to suit the
twine boxes, and again many are made to a specified
weight.
It will thus be seen that a series of balling machines
will be required to deal with the making up of the
twine in this form. These machines make neat and
attractive-looking balls, the weight of which may vary
from 2 oz. to 28 lb. each.
The mechanism by means of which the yarn is built
up into balls is at once elegant and ingenious, and the
made-up ball is quite satisfactory if when commencing
to use the twine, the end is withdrawn from the right
end of the ball. A ticket with the words “pull out this
end” is often attached as a guide. If the twine is drawn
from the wrong end of a ball, the continual difficulty
experienced in withdrawing the twine will be always remembered;
on the other hand, if the twine is drawn
out at the proper end, the correct running of the twine
will enable the attendant to complete his parcel tying
with the minimum of trouble and time, and enable him
to give attention to other work in hand.
This inconvenience is obviated by a comparatively
recent introduction in winding which makes an elegant
cylindrical structure termed a roll. This popular and
efficient mechanism is the Universal Winding Machine,
the various makes of which enable rolls of from 2 oz.
to 72 lb. to be made perfectly. The rolls are so attractive,
compact, economical and easily handled that one
would not be surprised to see a much more extended
application of this useful form of package.
For shops and similar places, the smaller balls and
rolls are made up in paper parcels of about 12 lb. each.
The larger balls and rolls may be made up separately
or in convenient numbers. Sewing threads and yarns
may be made up in small balls, but a more common and
neater arrangement is to make them up on reels or in
rolls. Neatness, facility for use, and suitability for
intended purposes are the main points to be cultivated
in order to secure and retain business.
Printed by Sir Isaac Pitman & Sons, Ltd., Bath, England v—(1465f)
Stephen Cotton & Co.LTD. Brookfield Foundry Belfast
Flax and Hemp
Textile Machine
Makers, Iron and
Brass Founders
SPECIALITIES:
¶ Patent Automatic Screwing and Changing Apparatuses
for Hackling Machines. Brush and Doffer Hackling
Machines. Stripper Rod Hackling Machines. Hand
and Power Reels, with Straight and Cross Winding.
Flax and Hemp Cutters. Bundling Presses. Spinning
Frames. Spindles and Flyers.
PARTICULARS ON APPLICATION
PITMAN’S
Common Commodities and Industries Series
Some Recent Additions. Each 2/6 net
THE BOOT AND SHOE INDUSTRY. By J. S. Harding, Head of the Boot Department of the Leeds Central Technical School.
FURNITURE. By H. E. Binstead, Editor of “The Furniture Record.”
COAL TAR. By A. R. Warnes, F.C.S., A.I.Mech.E., Lecturer on Coal Tar Distillation at Hull Technical College.
PETROLEUM. By A. Lidgett, Editor of the “Petroleum Times.”
SALT. By A. F. Calvert, F.C.S.
KNITTED FABRICS. By John Chamberlain, Head of the Textile Dept., Leicester Municipal Technical Schools, and James H. Quilter, late Editor of the “Hosiery Trade Journal.”
PAPER. Its History, Sources, and Production. By Harry A. Maddox, Silver Medallist Paper-making, 1909; City and Guilds Honours Typography, 1908-9; Contributor to leading trade journals.
SOAP. Its Composition, Manufacture, and Properties. By William H. Simmons, B.Sc. (Lond.), F.C.S., Lecturer on Soap Manufacture at the Battersea Polytechnic.
GLASS AND GLASS MAKING. By P. Marson, Consultant upon Refractory Materials, etc. Honours and Medallist in Glass Manufacture.
GUMS AND RESINS. Their Occurrence, Properties, and Uses. By Ernest J. Parry, B.Sc., F.I.C., F.C.S.
Complete List on application
SIR ISAAC PITMAN & SONS, LTD., 1 AMEN CORNER, LONDON, E.C.4
COMMON COMMODITIES AND INDUSTRIES SERIES
Each book in crown 8vo, cloth, with
many illustrations, charts, etc., 2/6 net
TEA. By A. Ibbetson
COFFEE. By B. B. Keable
SUGAR. By Geo. Martineau, C.B.
OILS. By C. Ainsworth Mitchell, B.A., F.I.C.
WHEAT. By Andrew Millar
RUBBER. By C. Beadle and H. P. Stevens, M.A., Ph.D., F.I.C.
IRON AND STEEL. By C. Hood
COPPER. By H. K. Picard
COAL. By Francis H. Wilson, M.Inst., M.E.
TIMBER. By W. Bullock
COTTON. By R. J. Peake
SILK. By Luther Hooper
WOOL. By J. A. Hunter
LINEN. By Alfred S. Moore
TOBACCO. By A. E. Tanner
LEATHER. By K. J. Adcock
KNITTED FABRICS. By J. Chamberlain and J. H. Quilter
CLAYS. By Alfred B. Searle
PAPER. By Harry A. Maddox
SOAP. By William A. Simmons, B.Sc. (Lond.), F.C.S.
THE MOTOR INDUSTRY. By Horace Wyatt, B.A.
GLASS AND GLASS MAKING. By Percival Marson
GUMS AND RESINS. By E. J. Parry, B.Sc., F.I.C., F.C.S.
THE BOOT AND SHOE INDUSTRY. By J. S. Harding
GAS AND GAS MAKING. By W. H. Y. Webber
FURNITURE. By H. E. Binstead
COAL TAR. By A. R. Warnes
PETROLEUM. By A. Lidgett
SALT. By A. F. Calvert
ZINC. By T. E. Lones, M.A., LL.D., B.Sc.
PHOTOGRAPHY. By Wm. Gamble
ASBESTOS. By A. Leonard Summers
SILVER. By Benjamin White
CARPETS. By Reginald S. Brinton
PAINTS AND VARNISHES. By A. S. Jennings
CORDAGE AND CORDAGE HEMP AND FIBRES. By T. Woodhouse and P. Kilgour
ACIDS AND ALKALIS. By G. H. J. Adlam
ELECTRICITY. By R. E. Neale, B.Sc., Hons.
ALUMINIUM. By Captain G. Mortimer
OTHERS IN PREPARATION
Transcriber’s notes
The illustrations have been moved to appropriate paragraph breaks. References to their page numbers in the List of Illustrations and the Index have been adjusted accordingly.
The footnotes have been renumbered and moved to the end of the chapter in which they occur. Index entries may refer to text in a footnote.
Some index entries have been changed where it seems the original page number was incorrect.
The reference to Fig. 10 on page 51 originally read Fig. 12.
The advertisements have been moved to the end of the book.
Obvious typographical errors have been corrected. Inconsistent hyphenation has not been changed.
Read Cordage and cordage hemp and fibres (1919) by Thomas Woodhouse — Full Text Online Free | Open Old Books
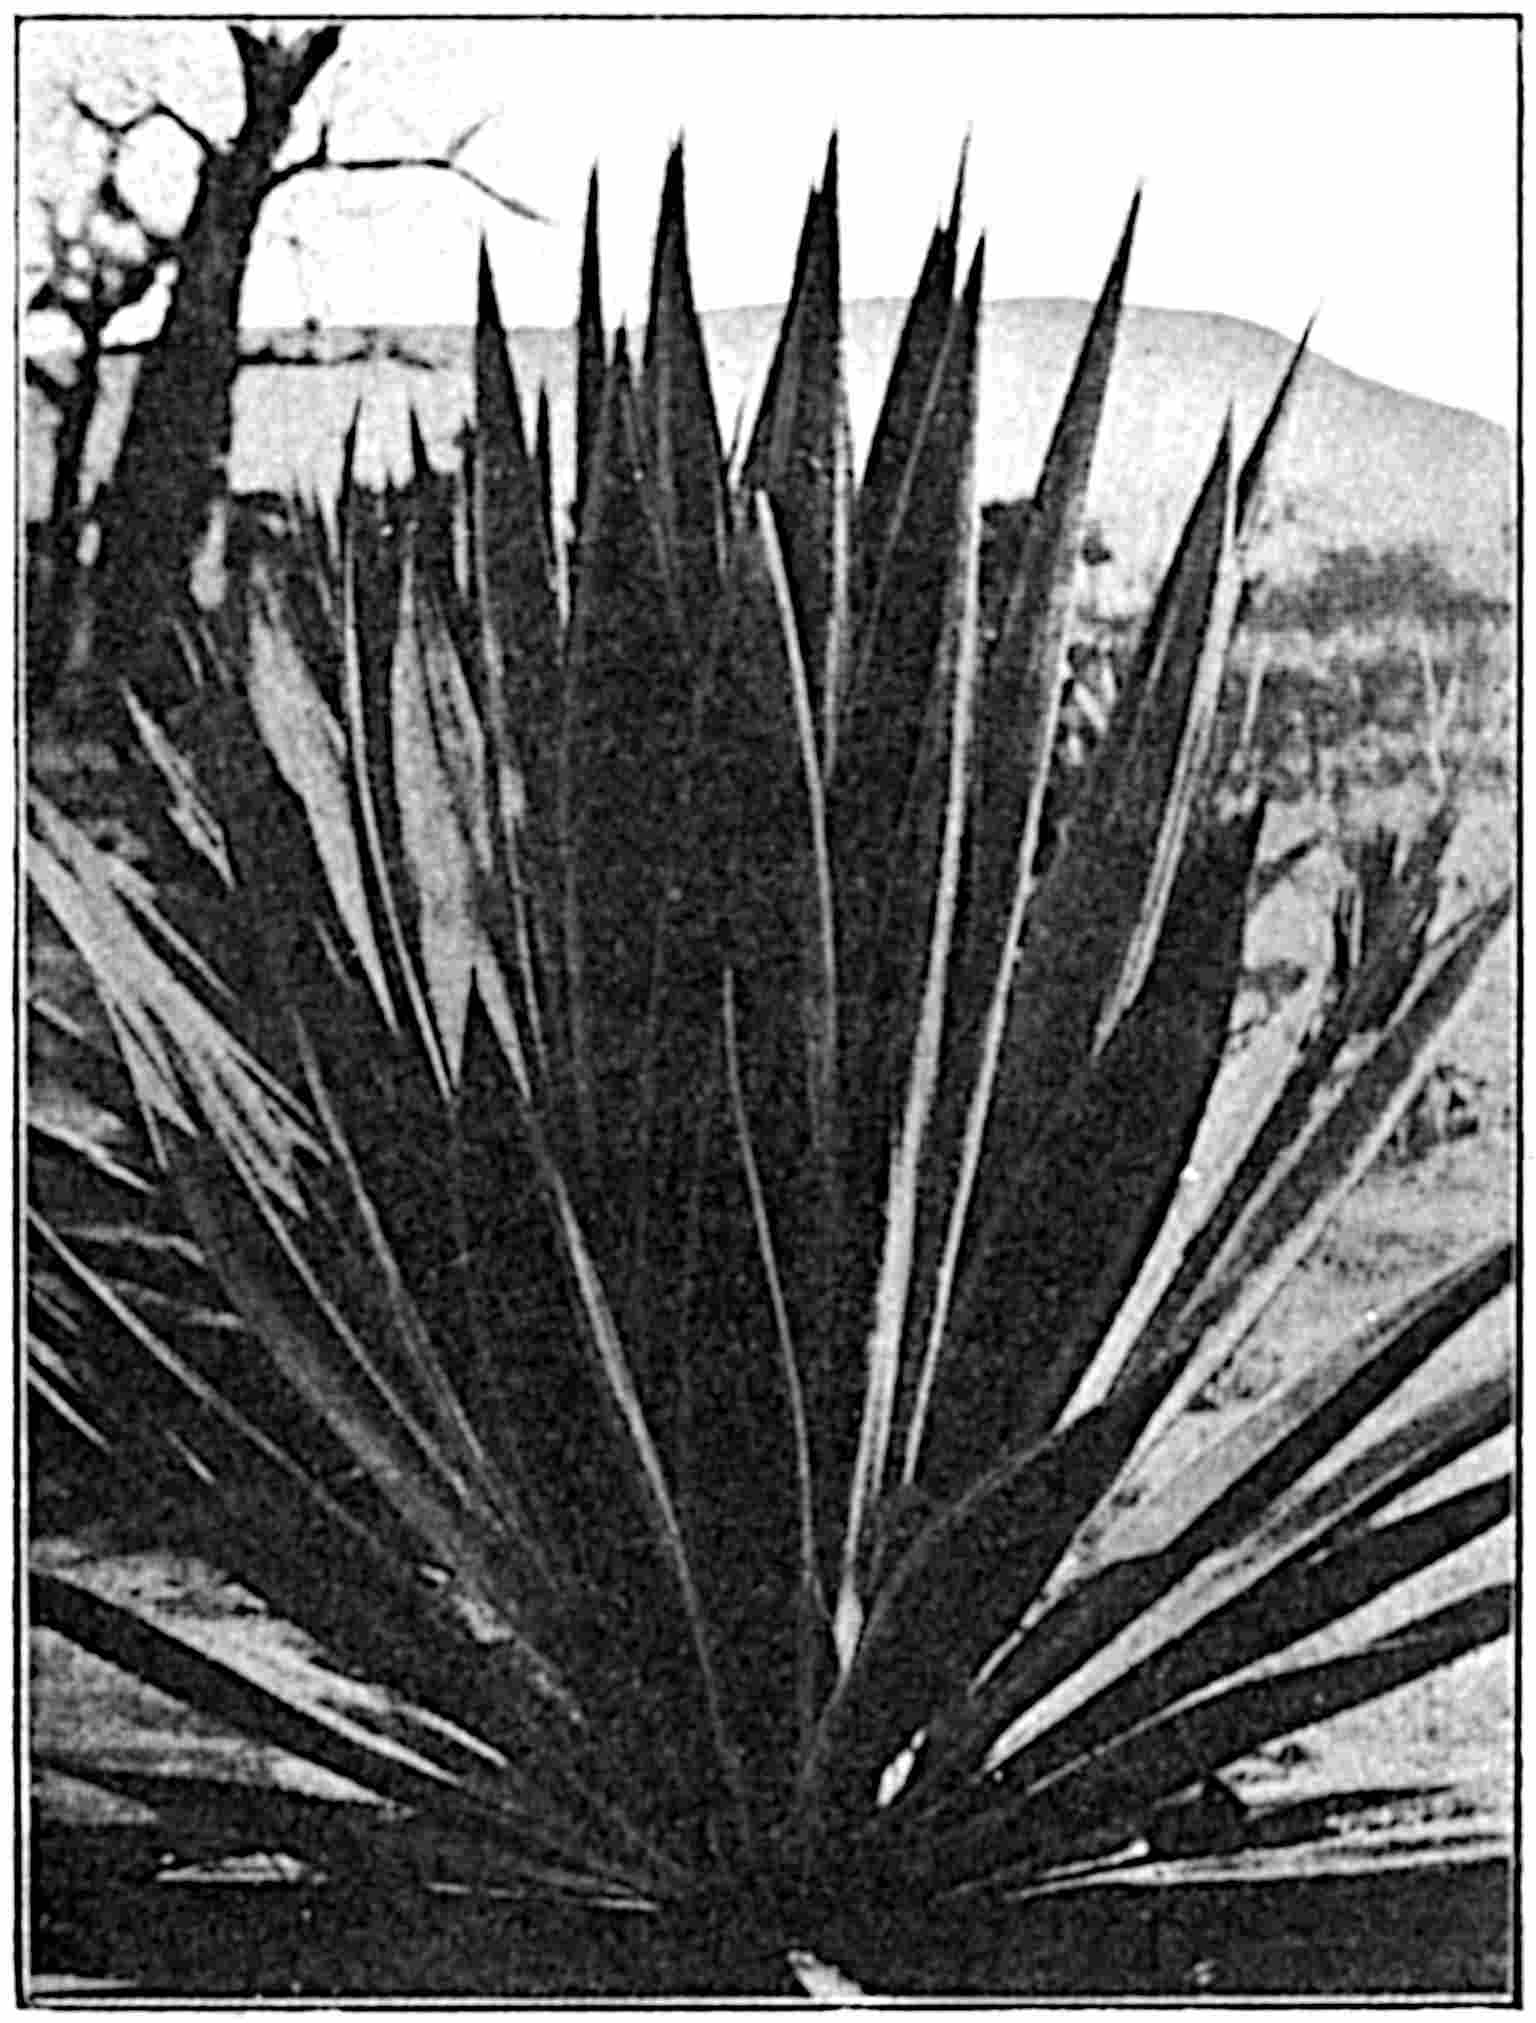
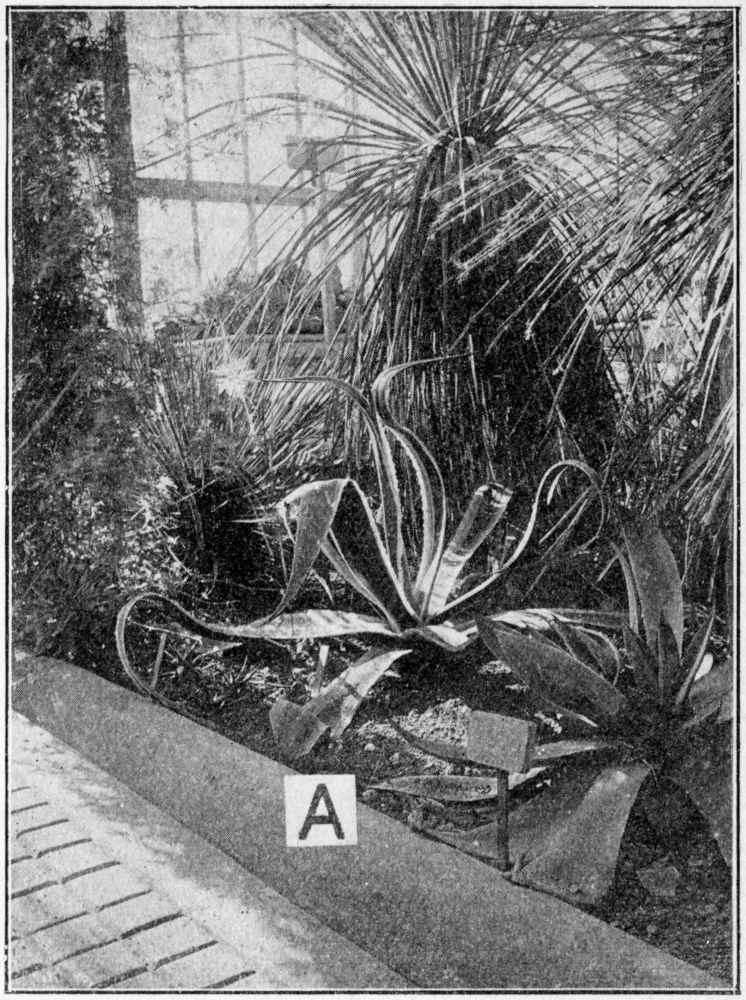
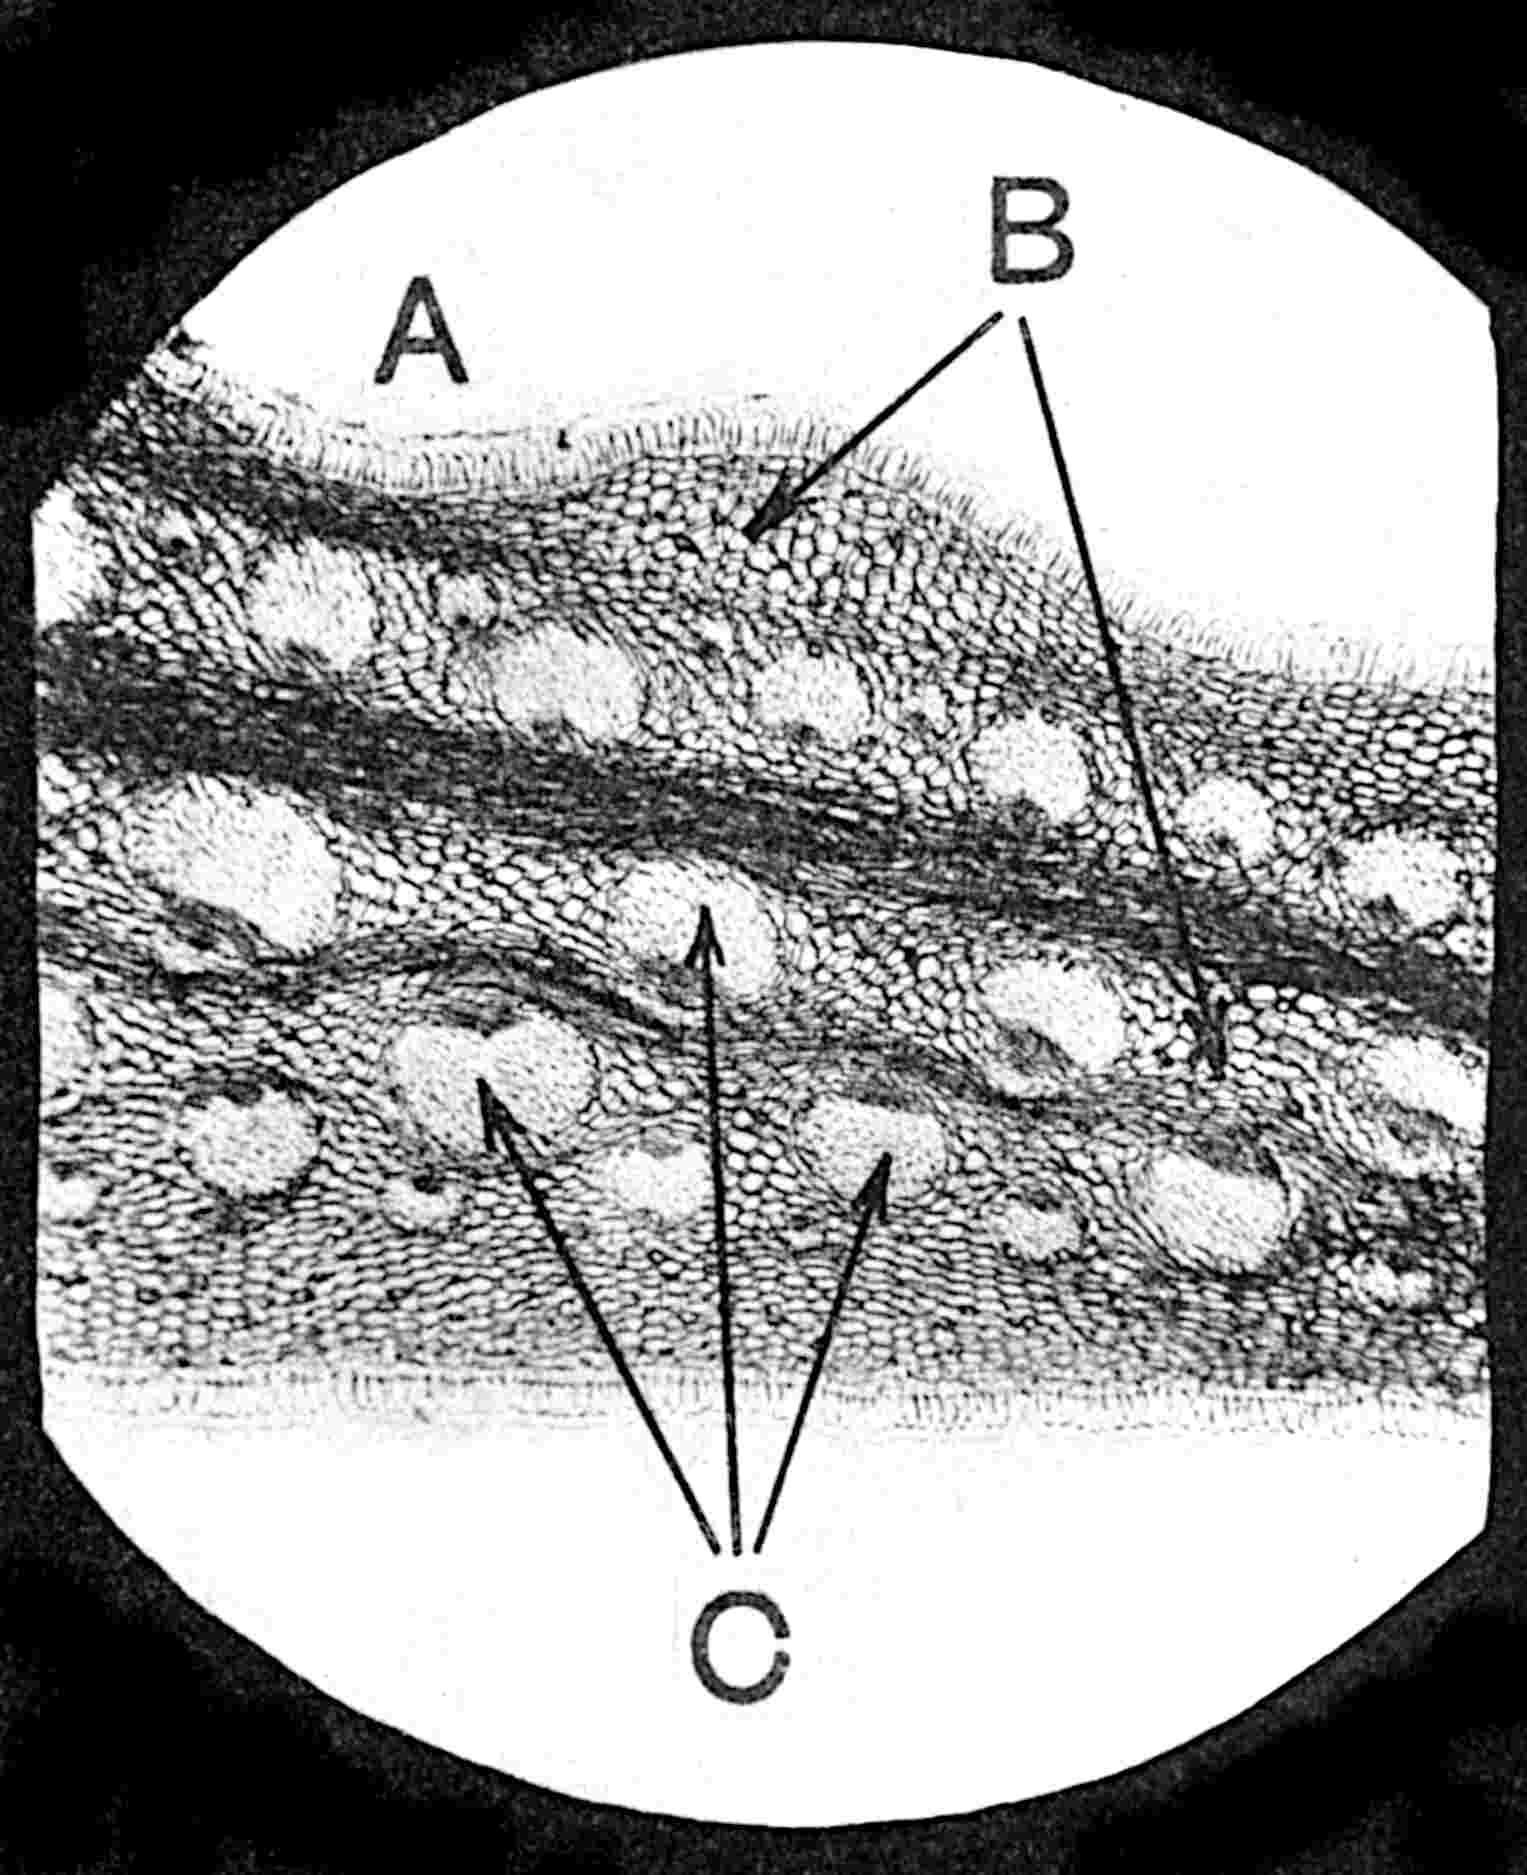
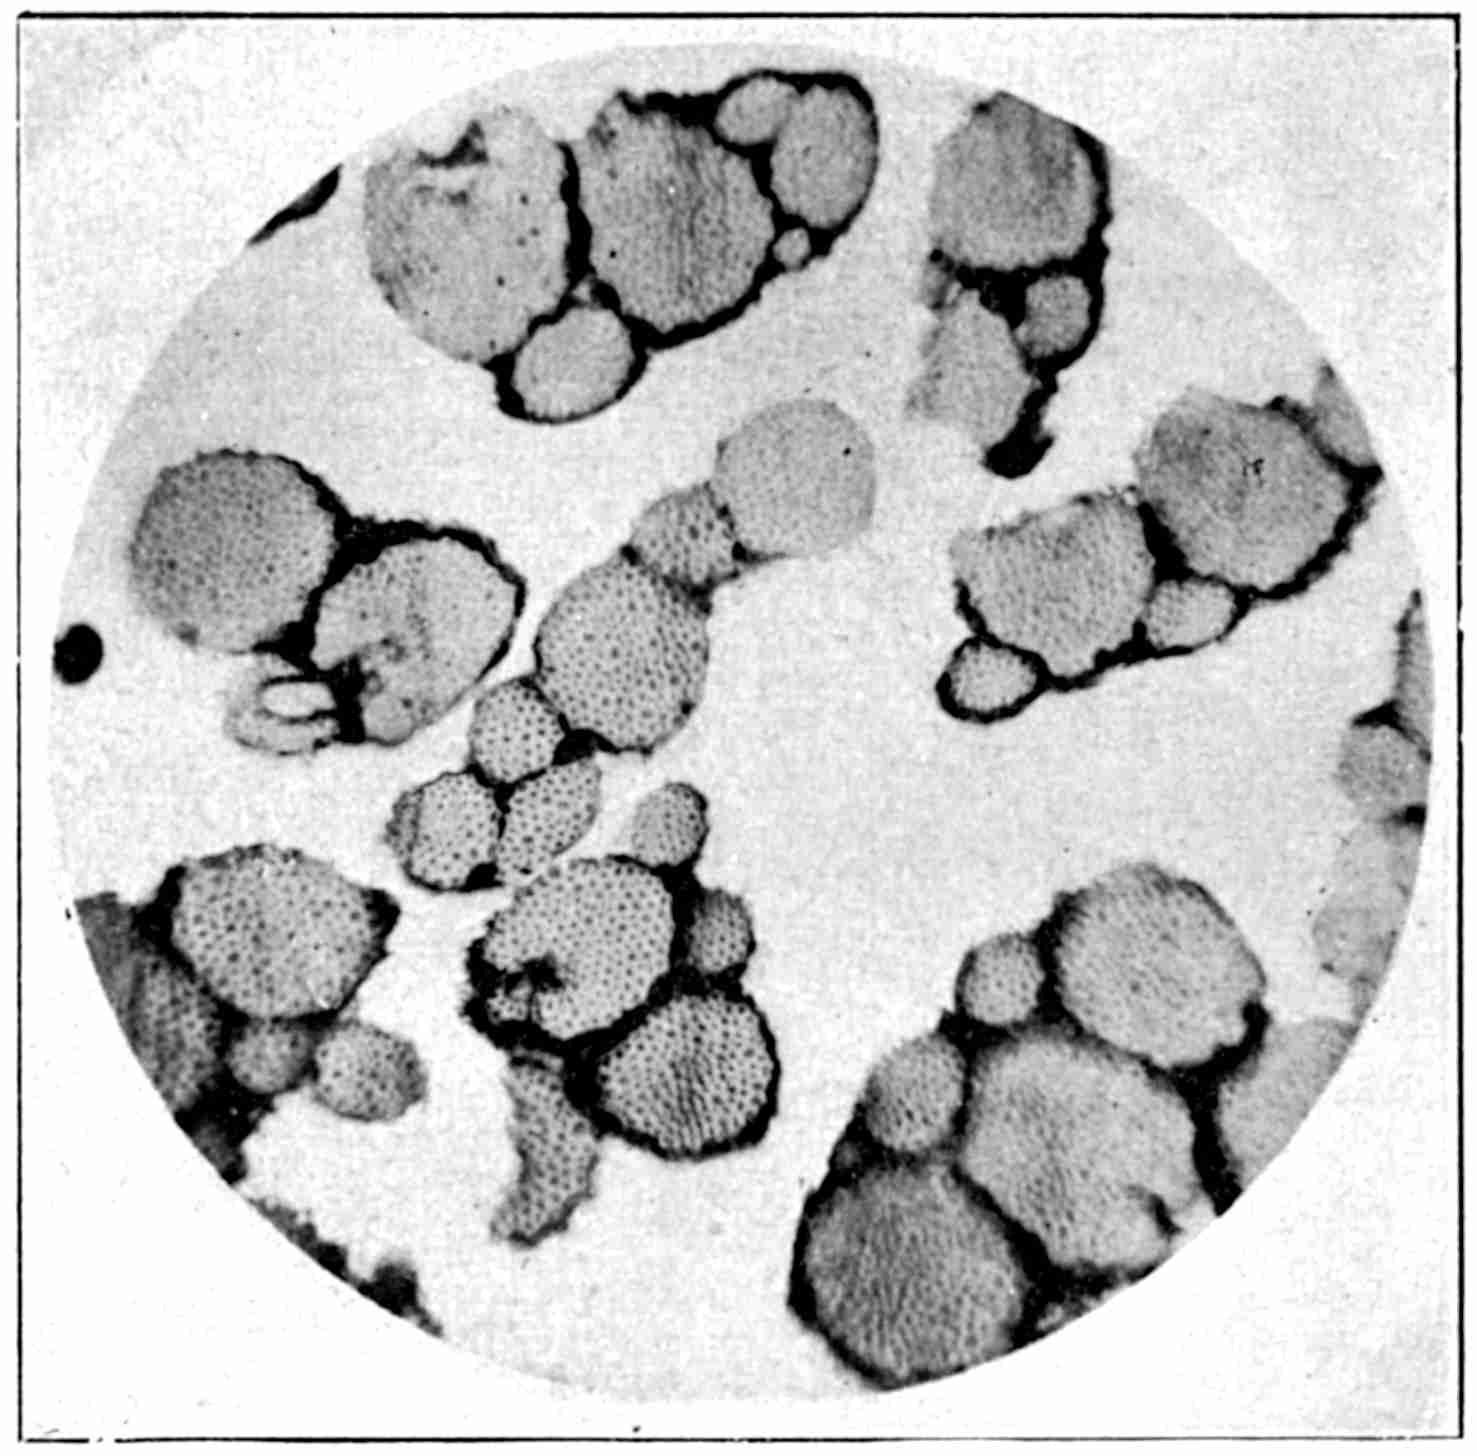
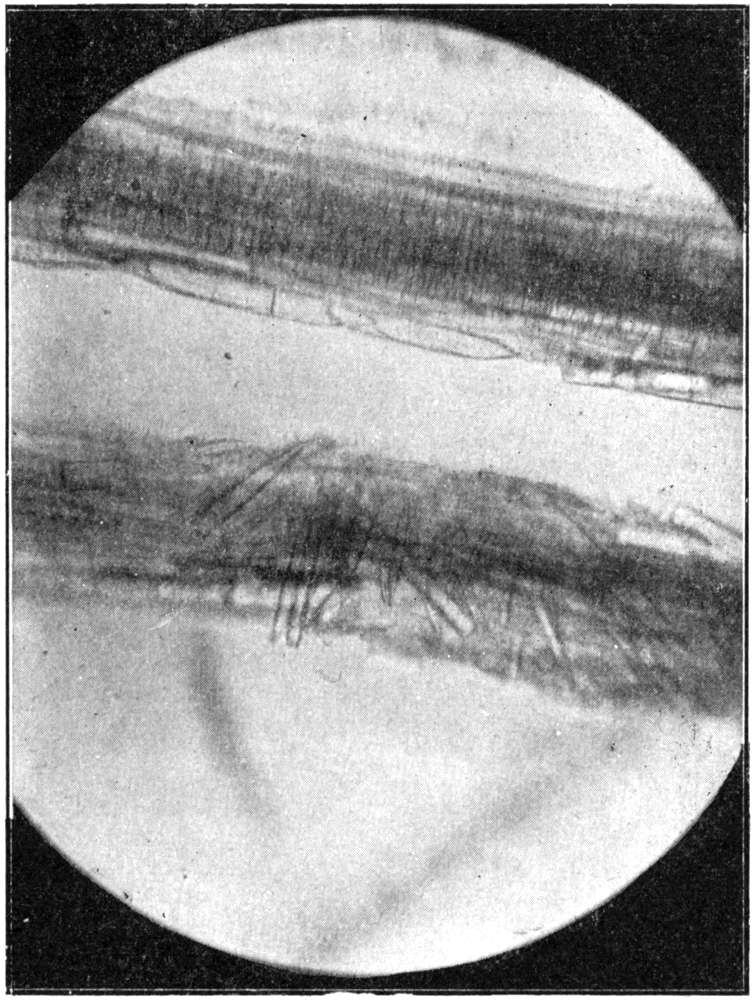
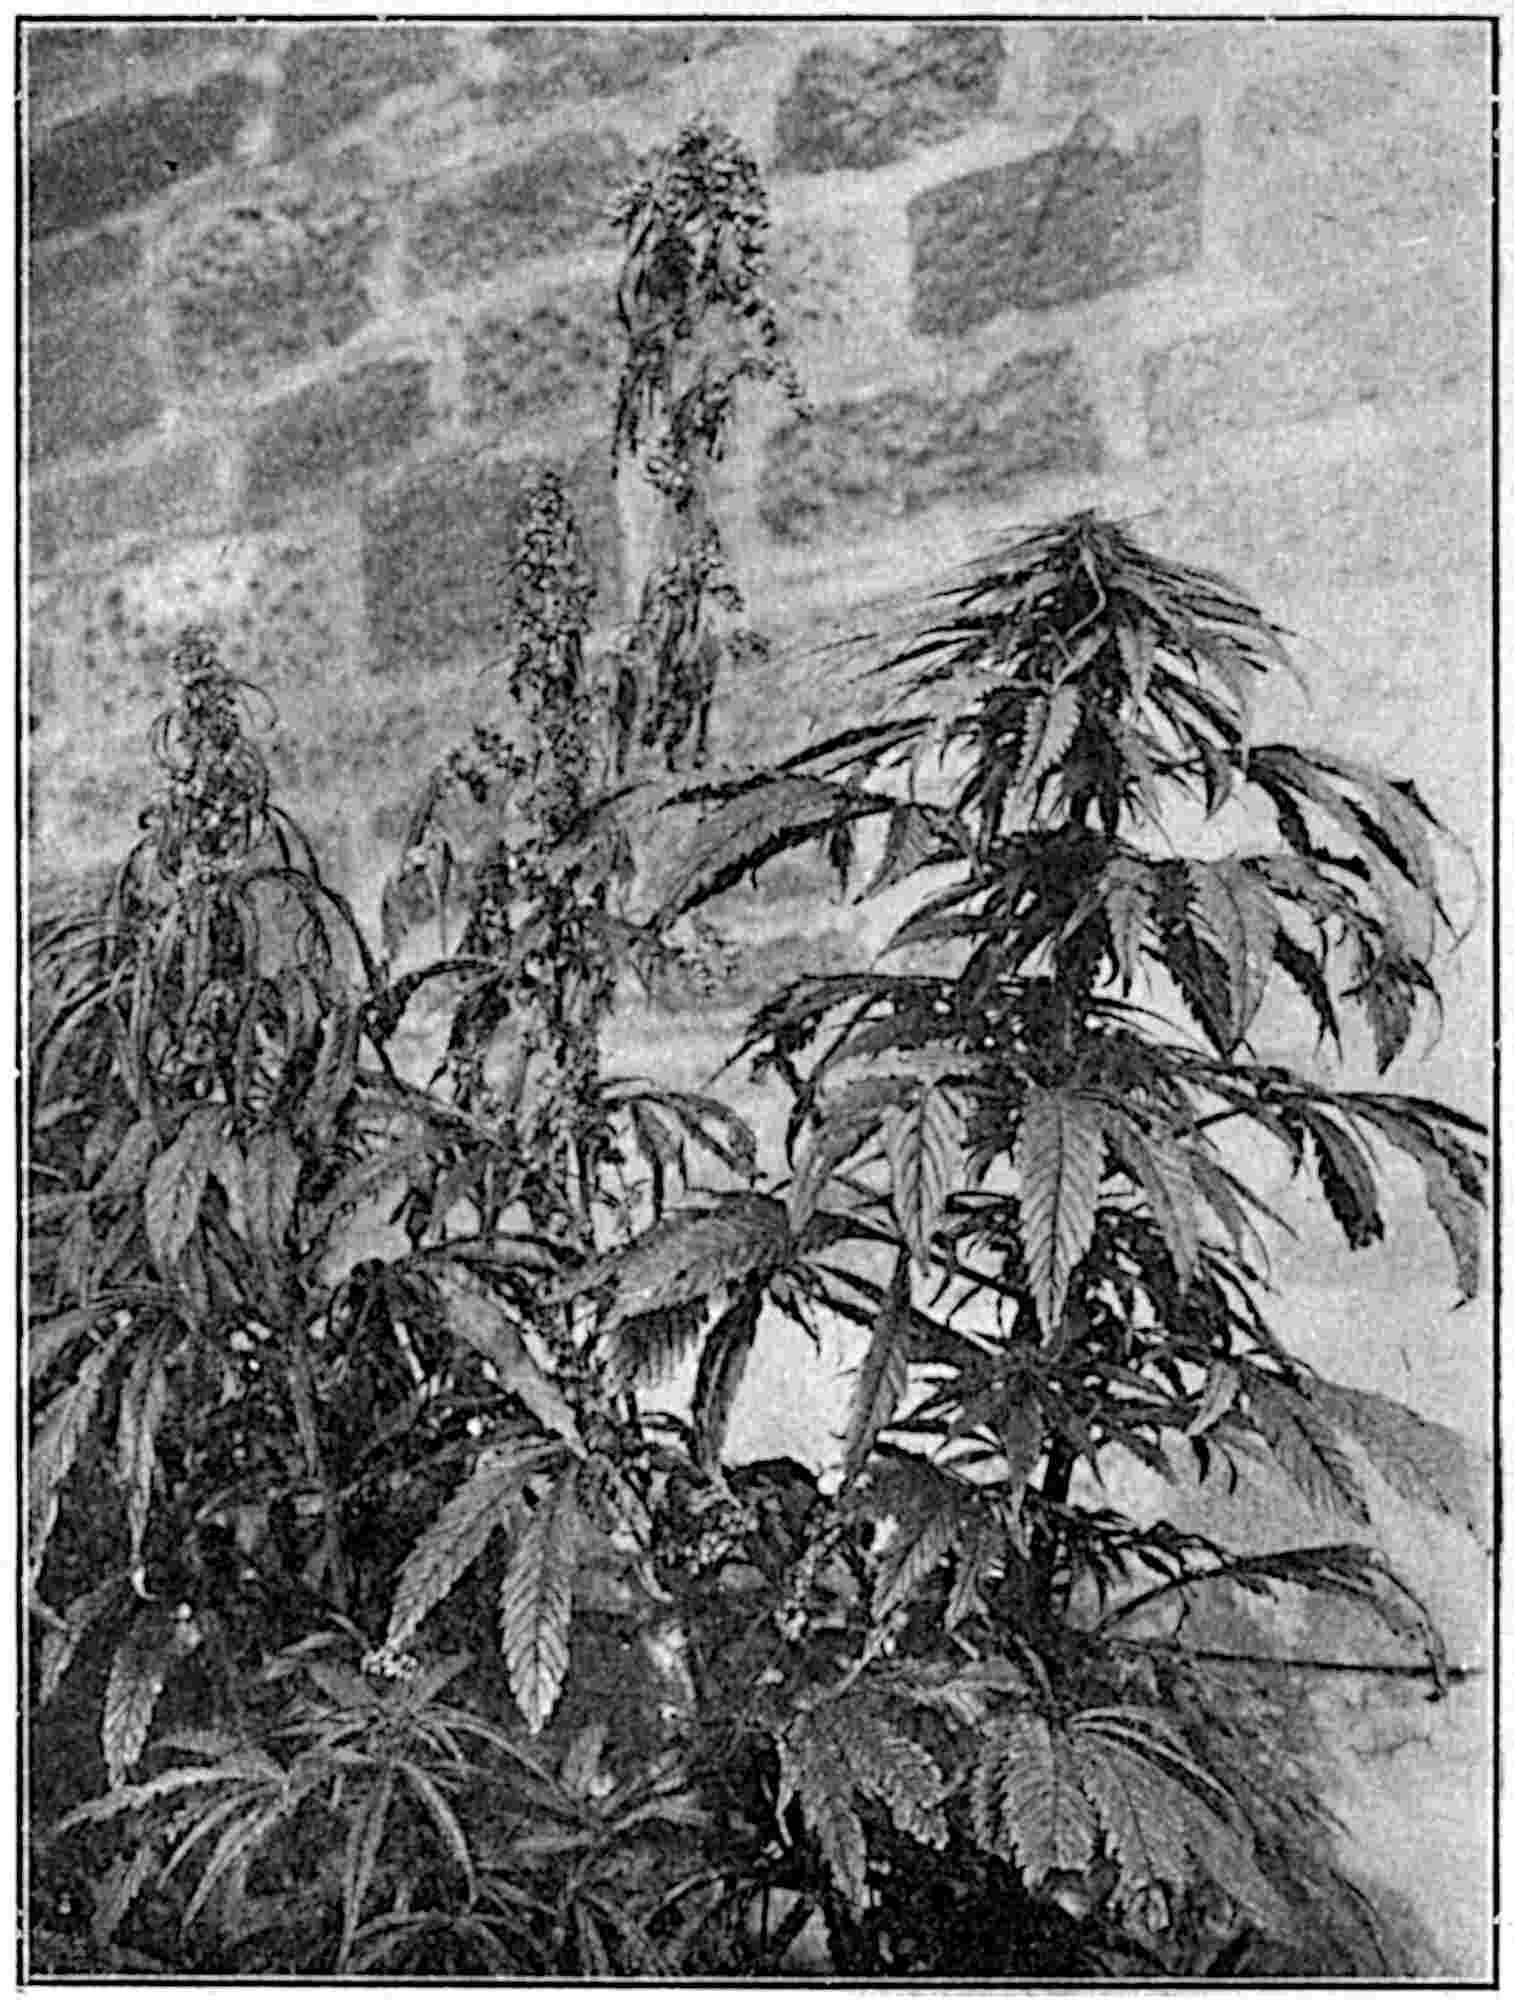
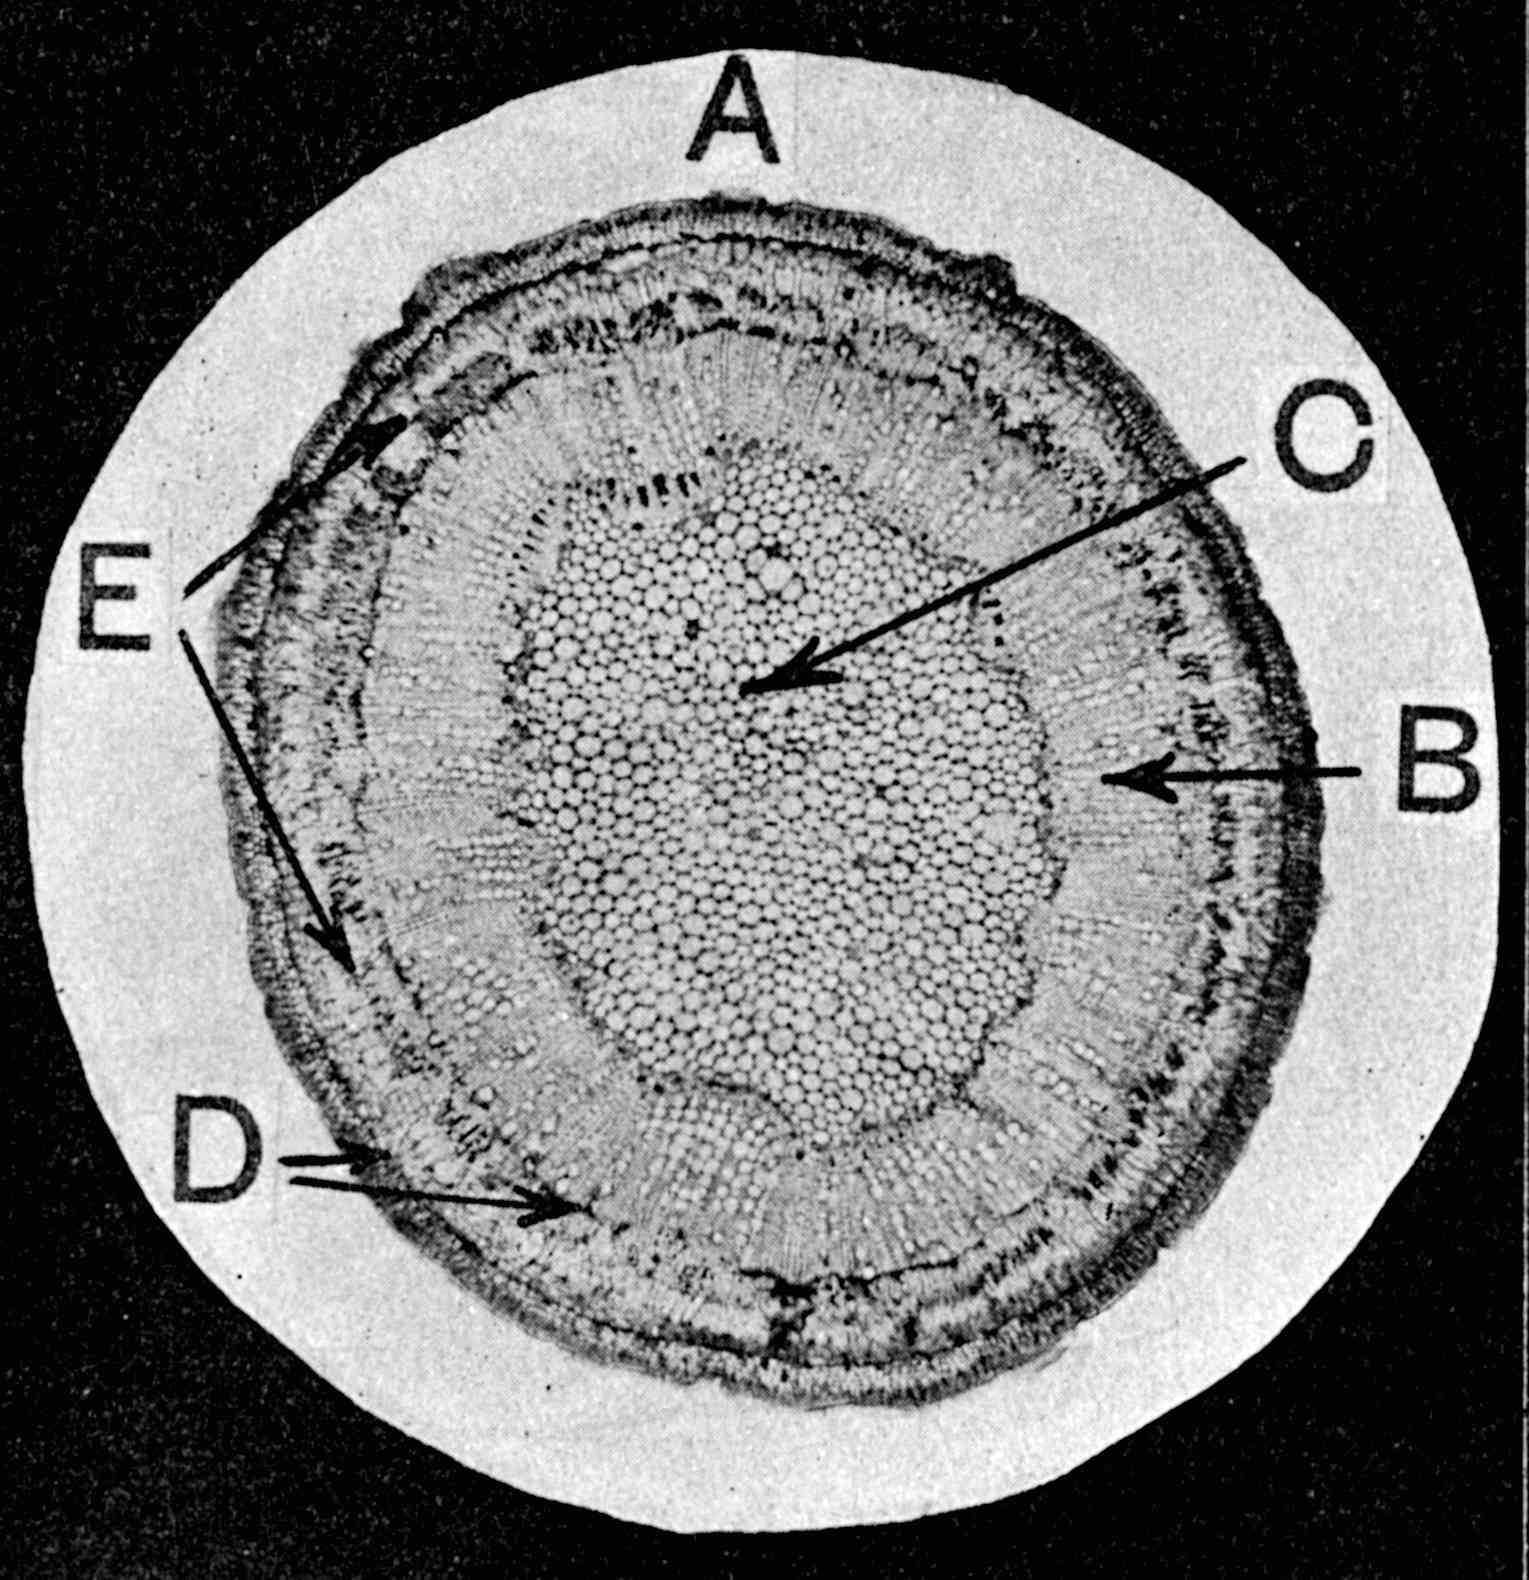
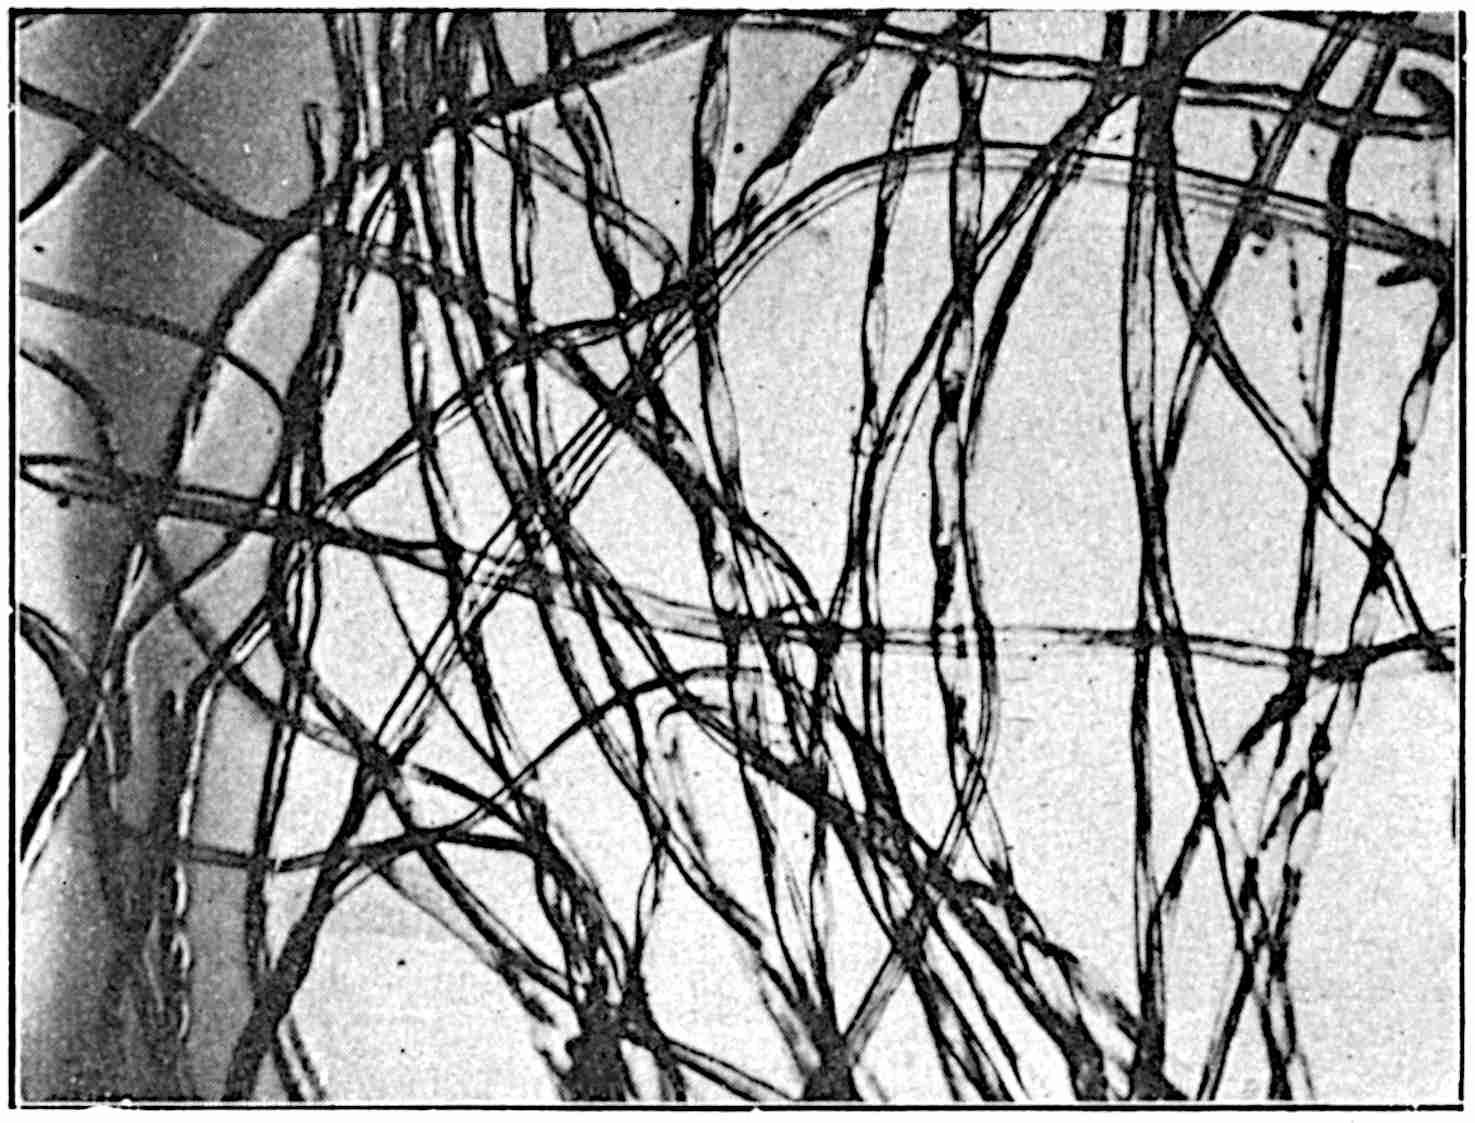
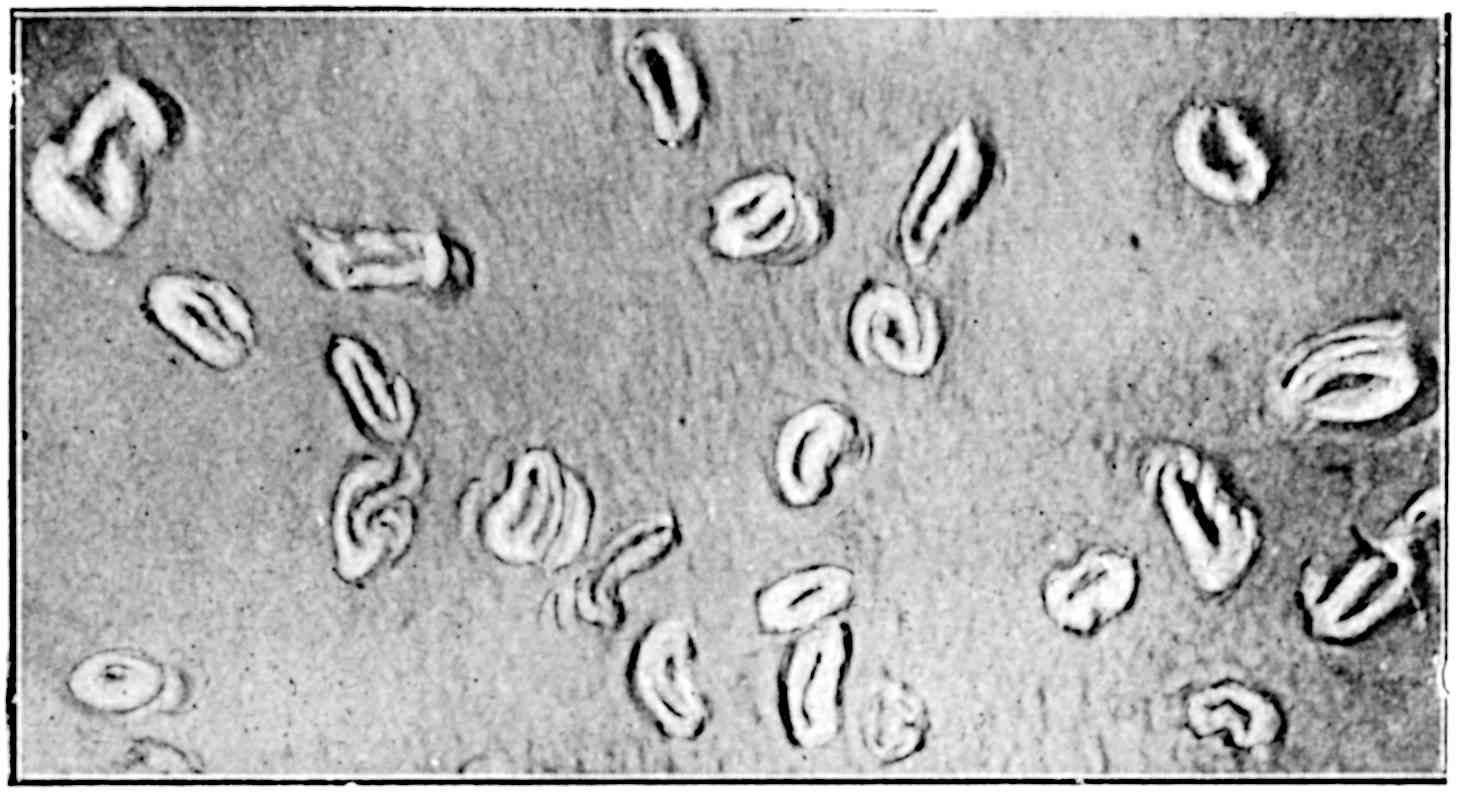
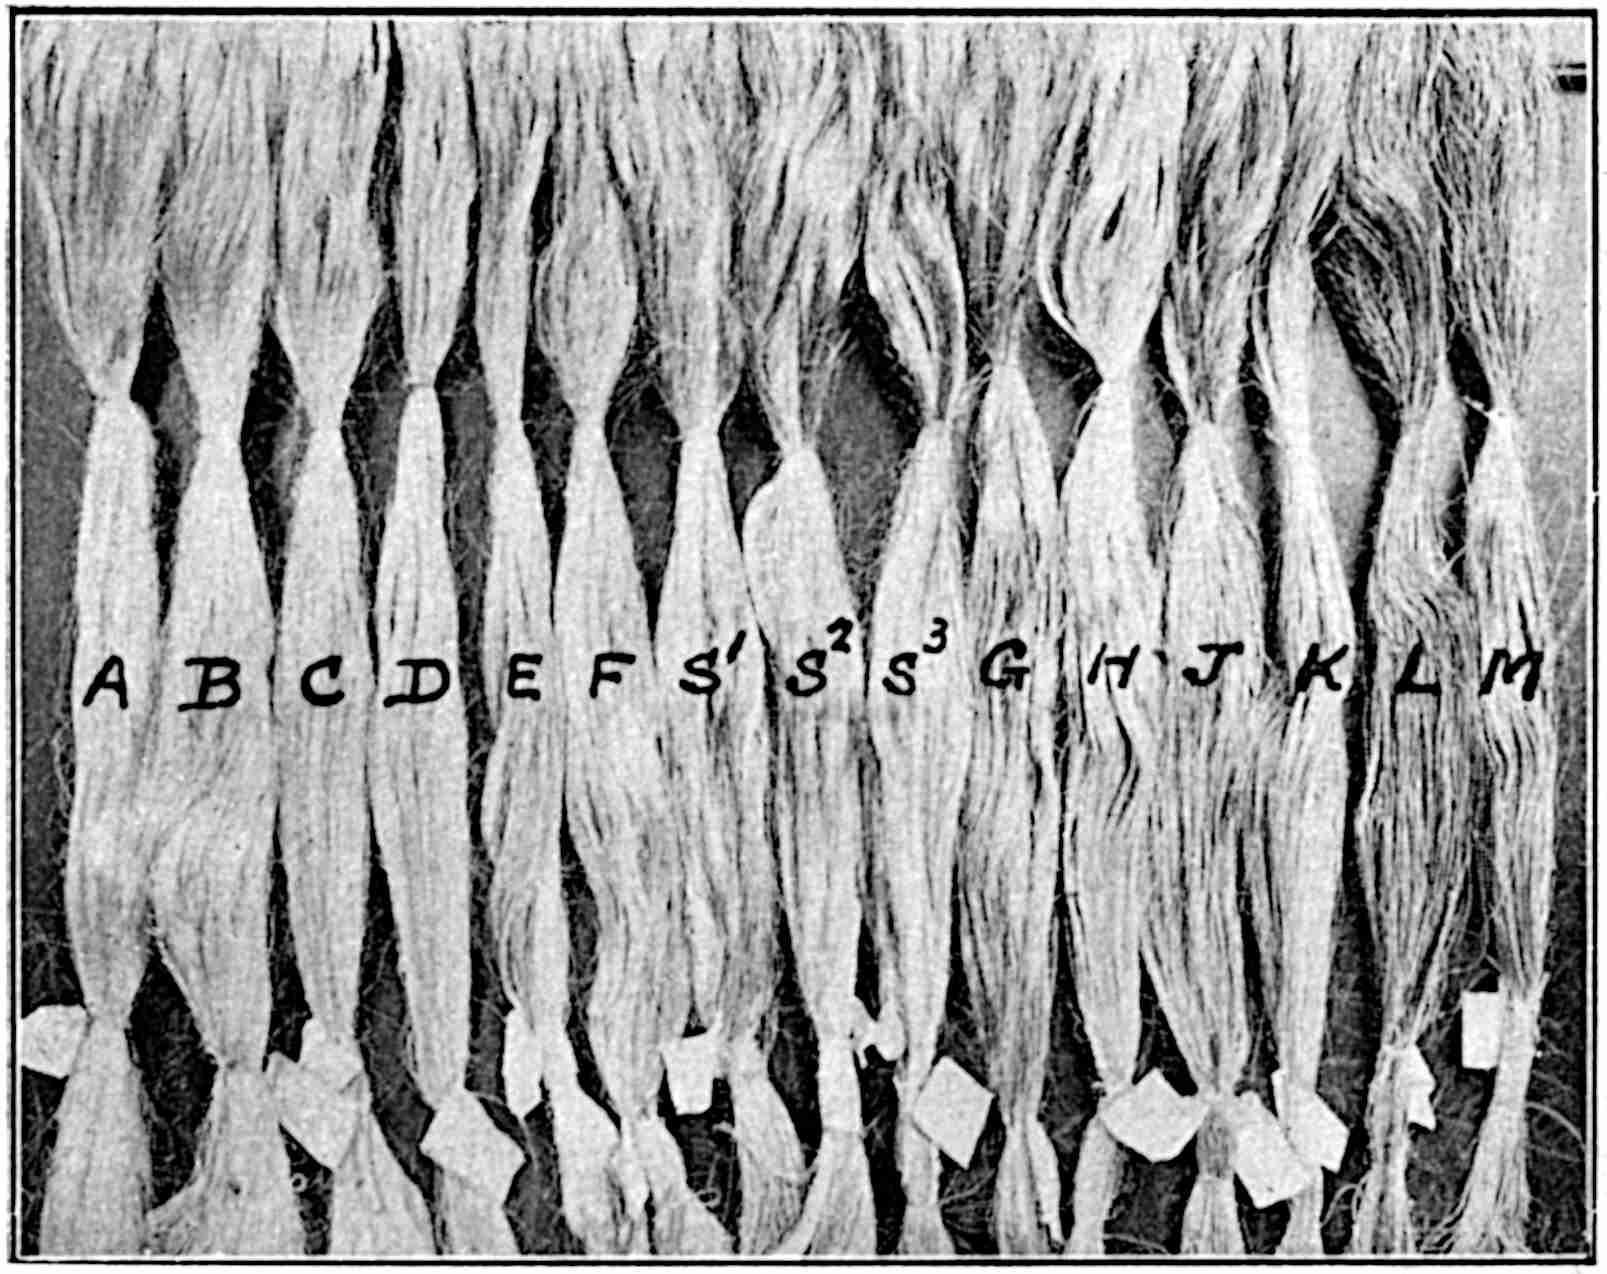
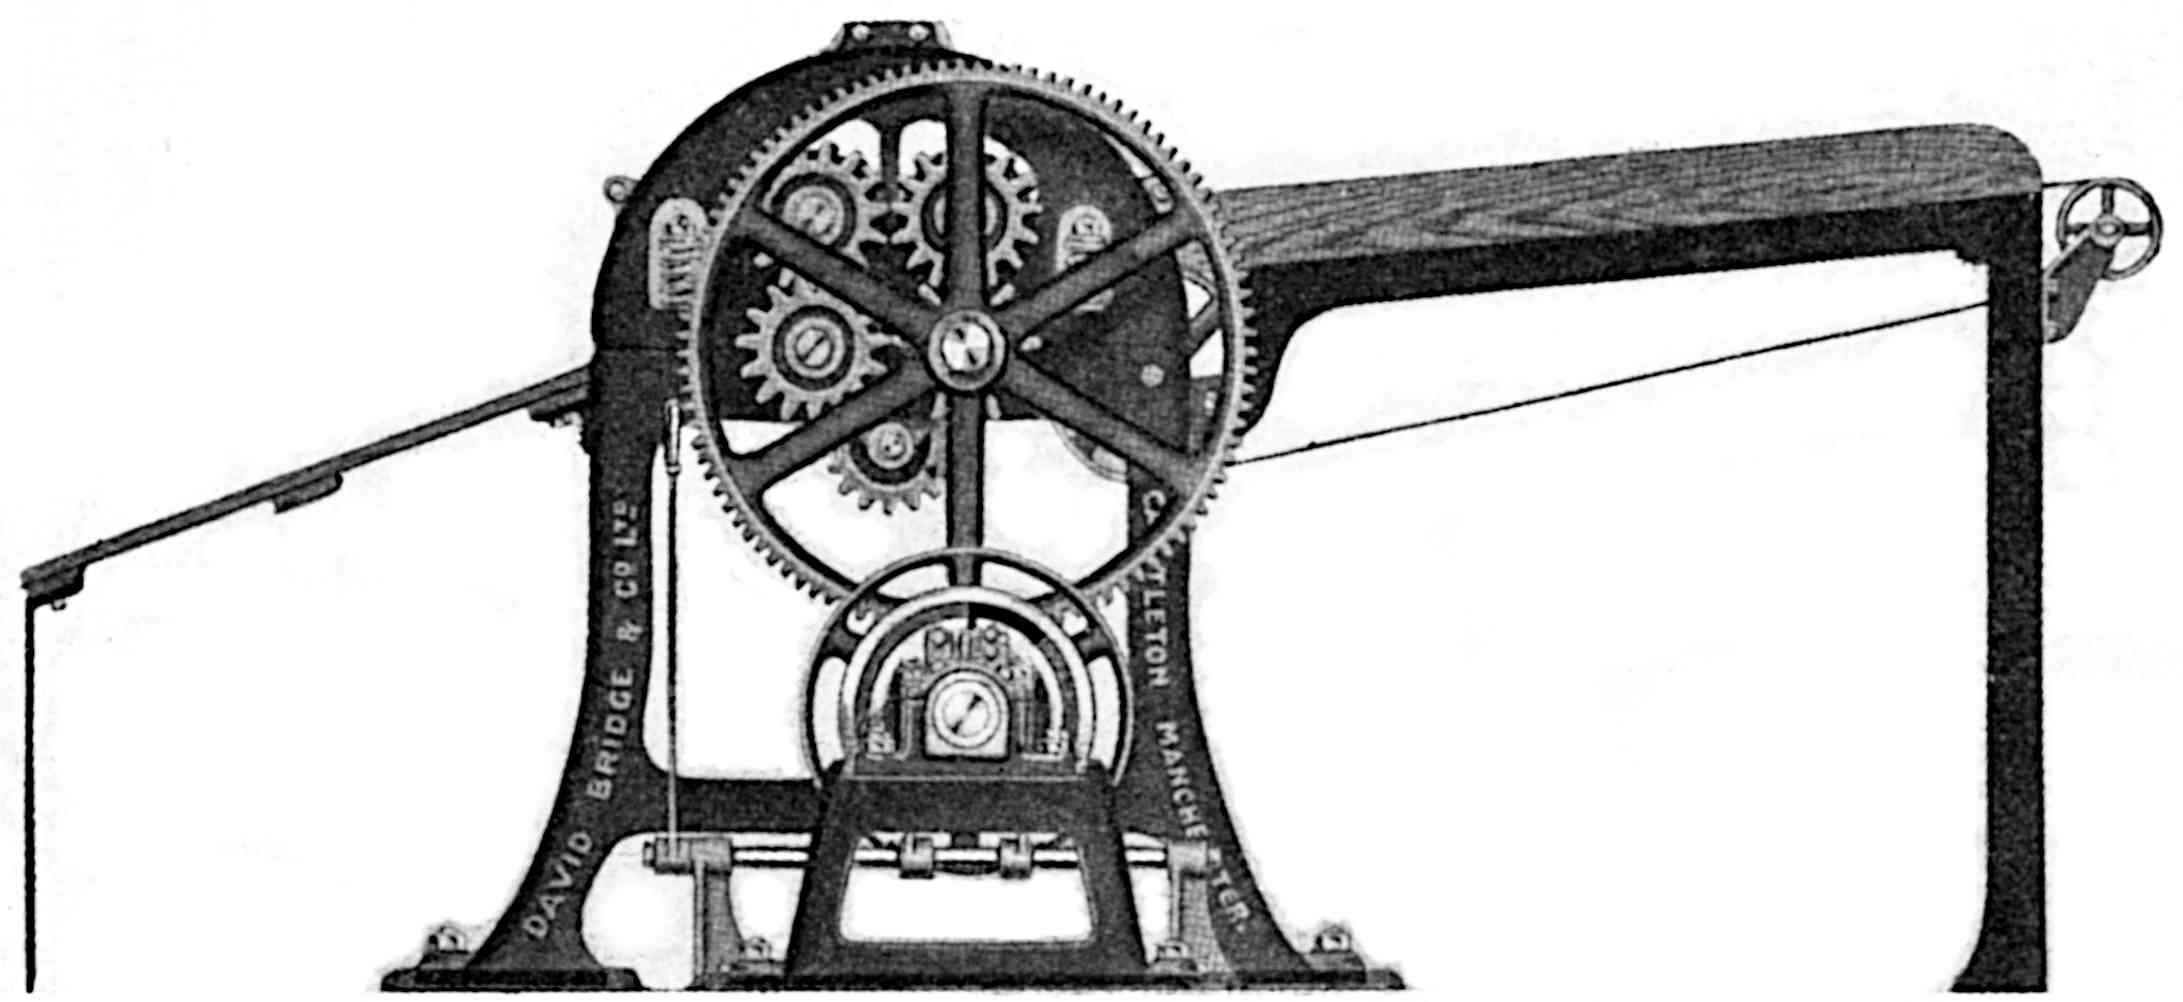
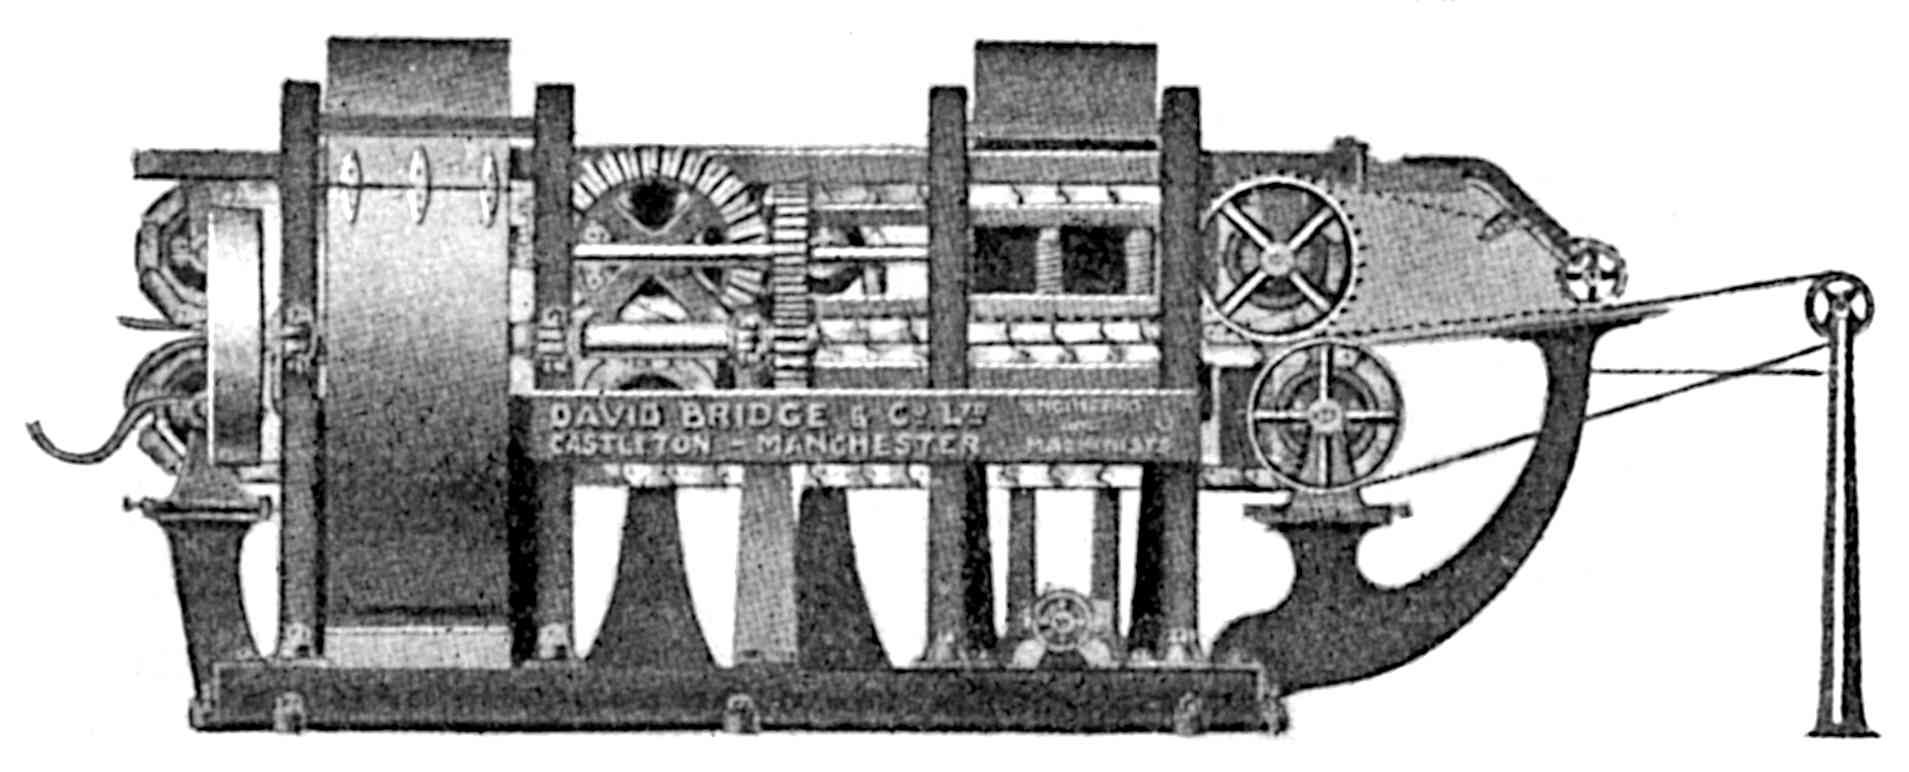
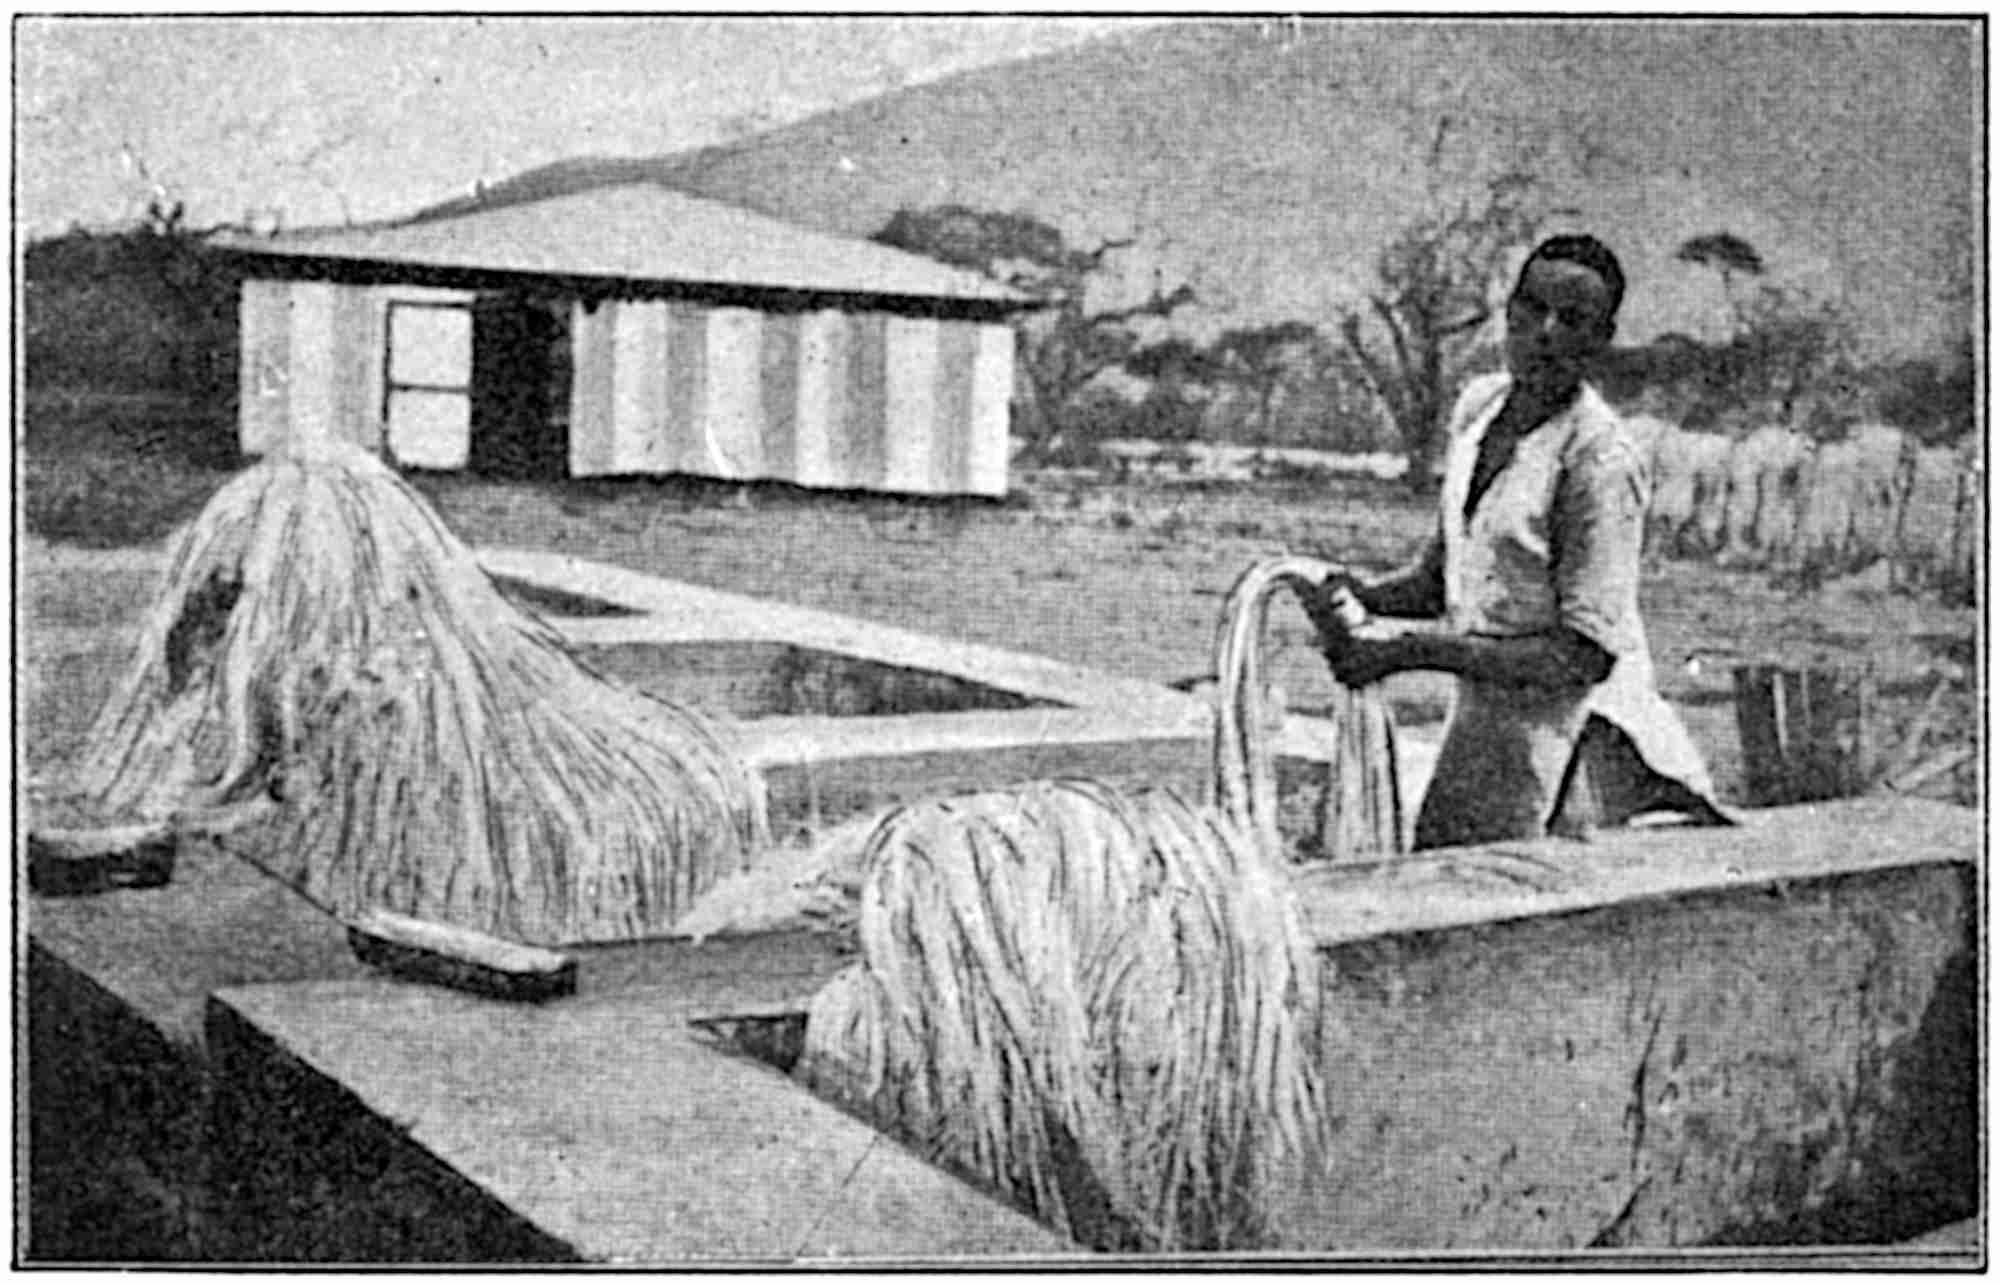
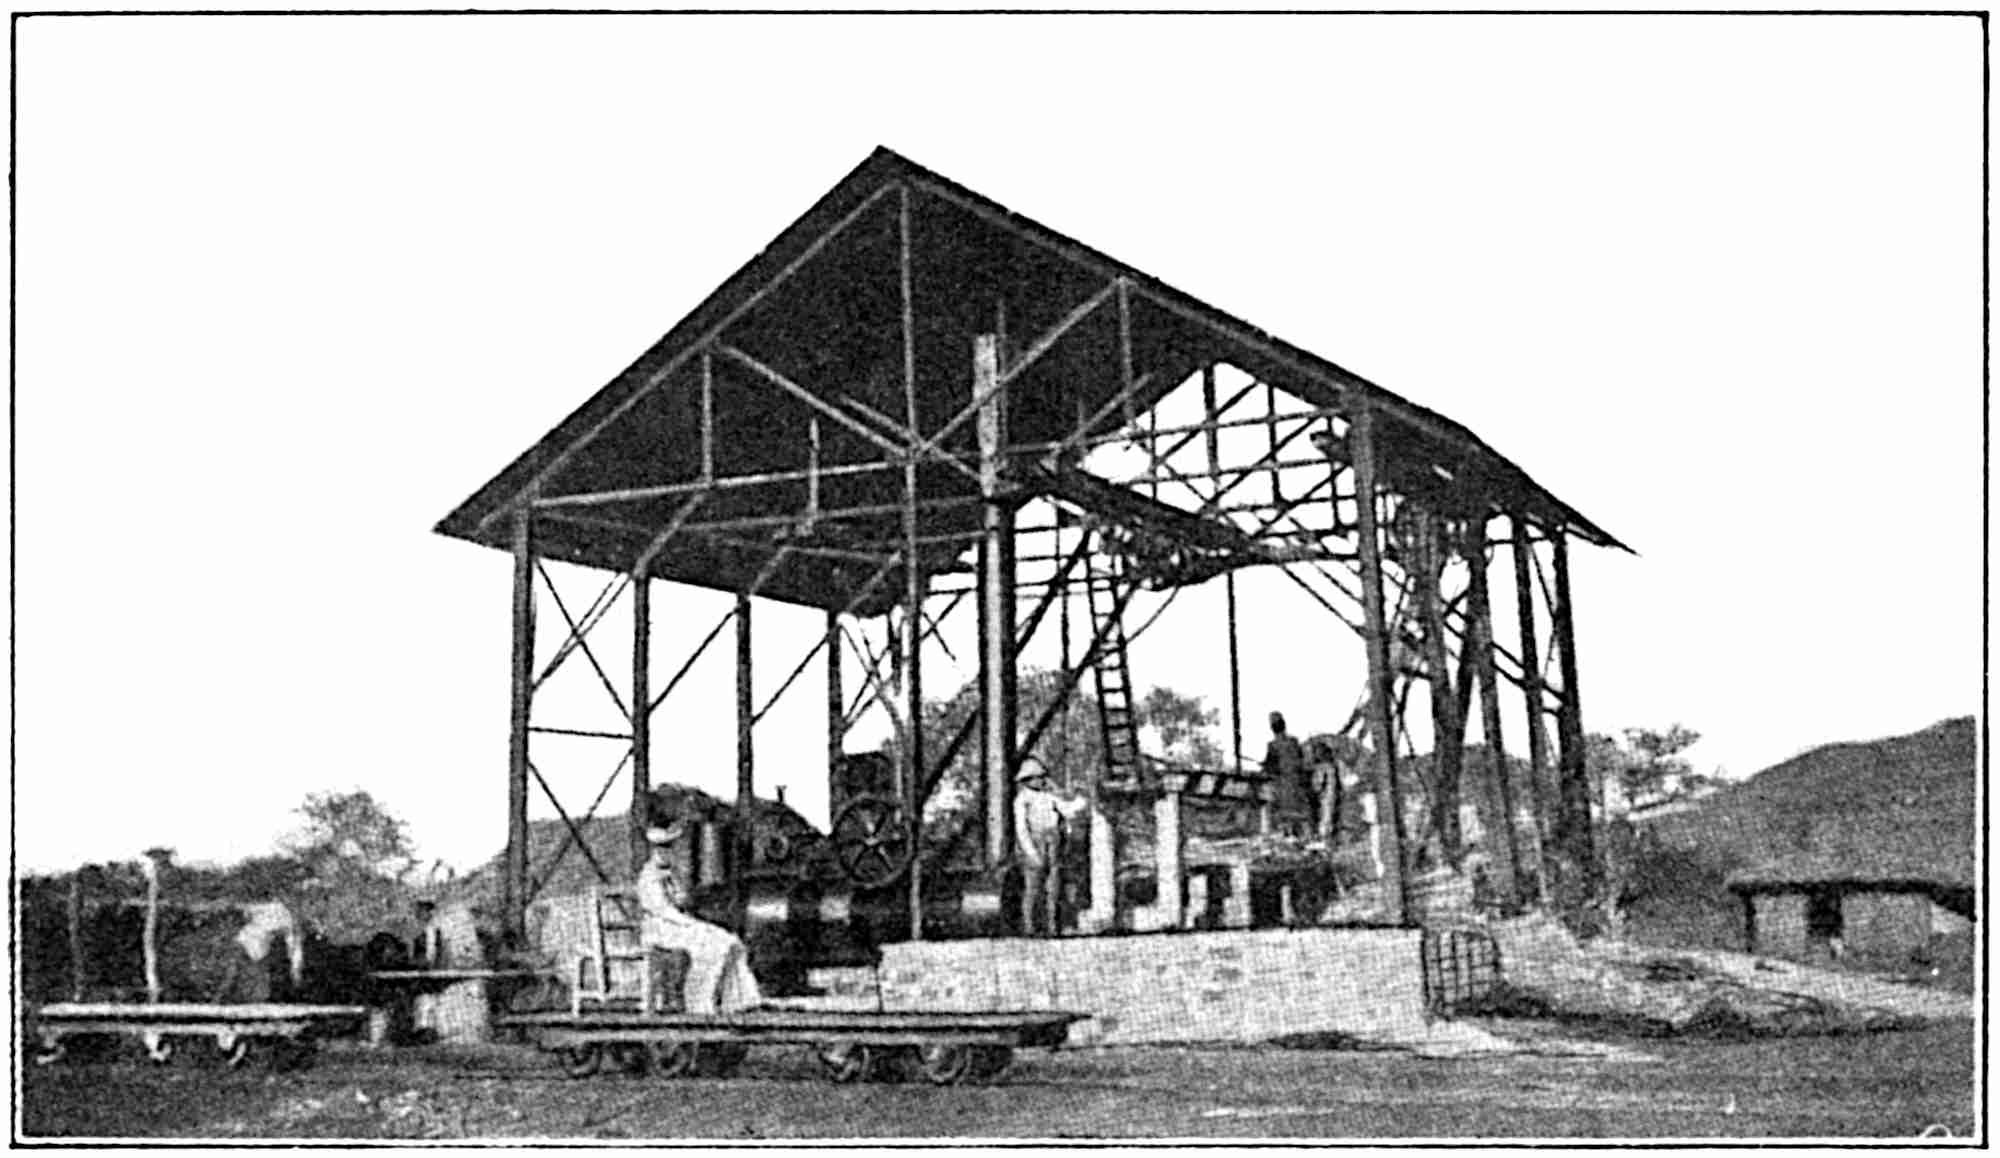
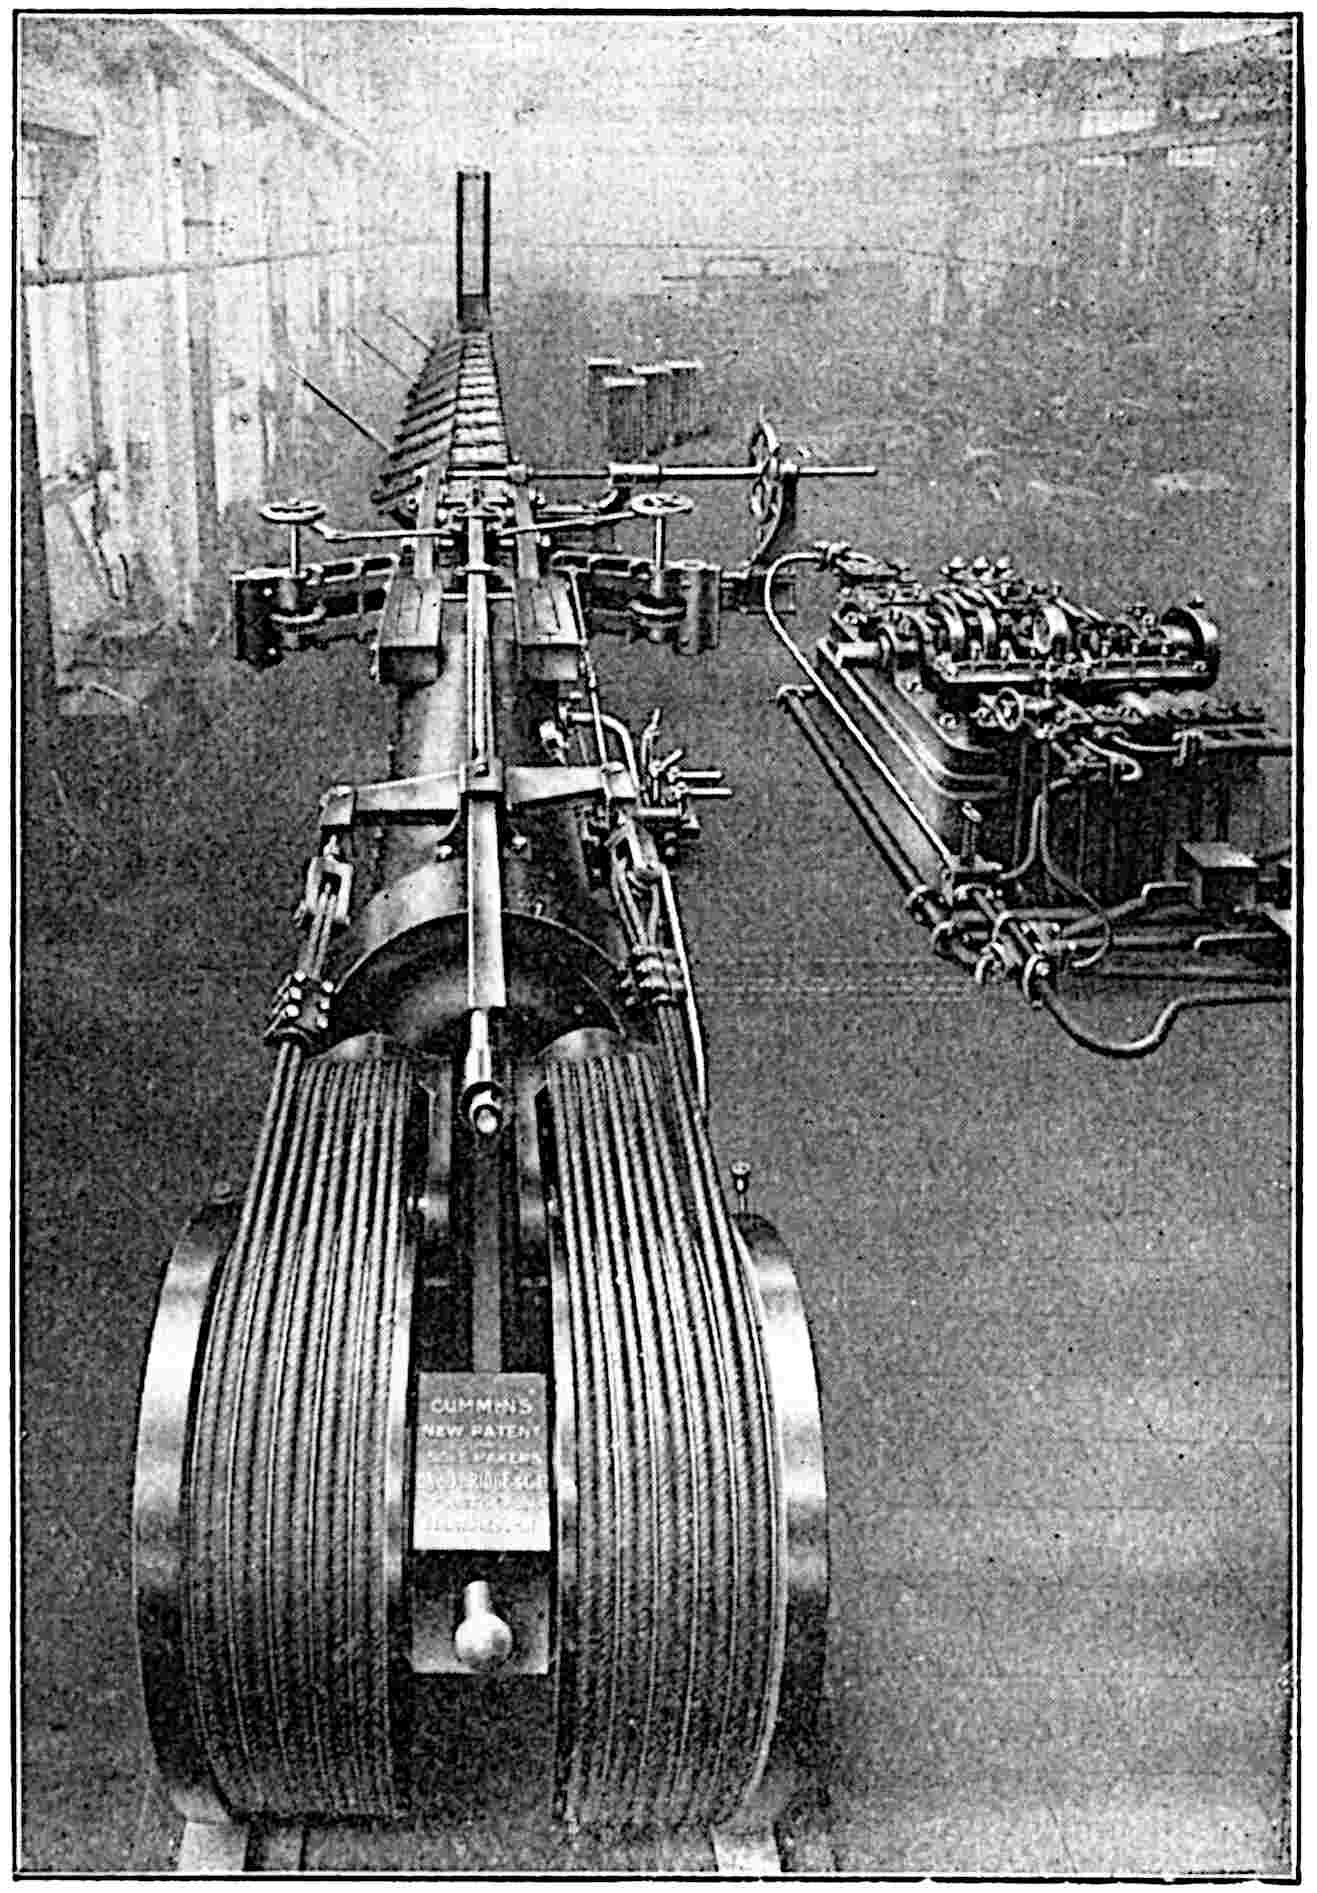
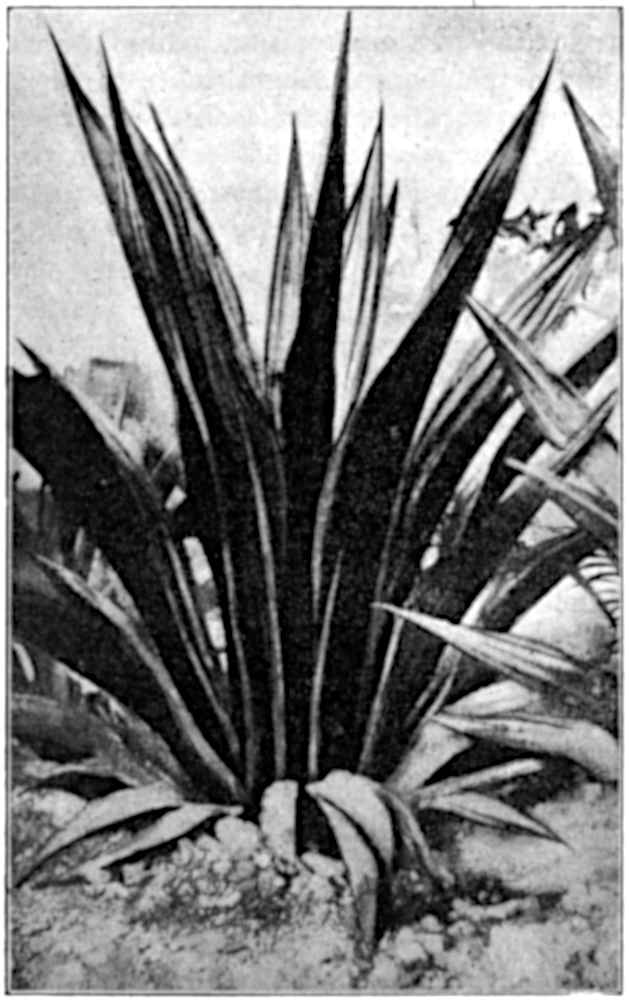
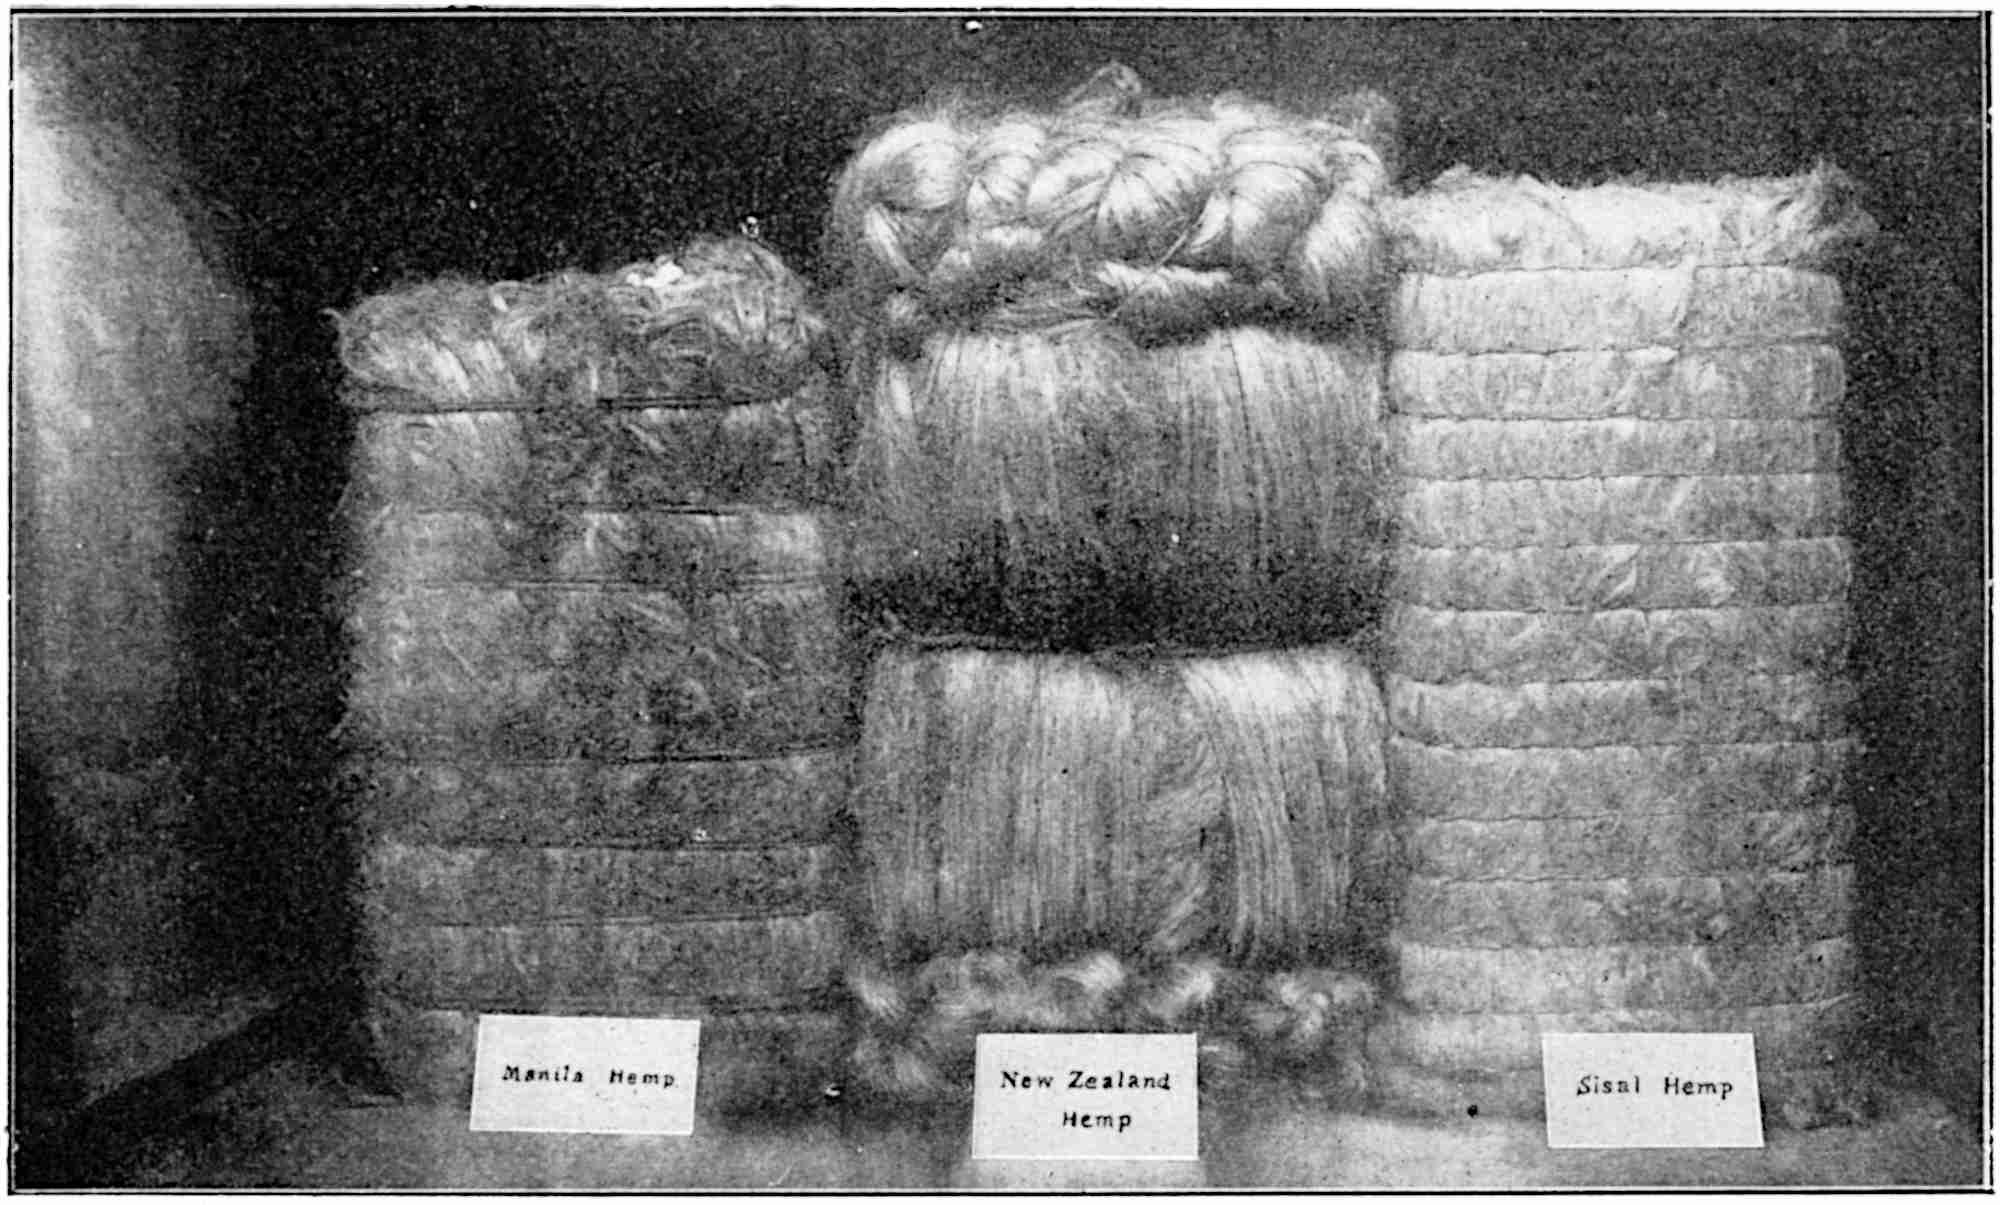
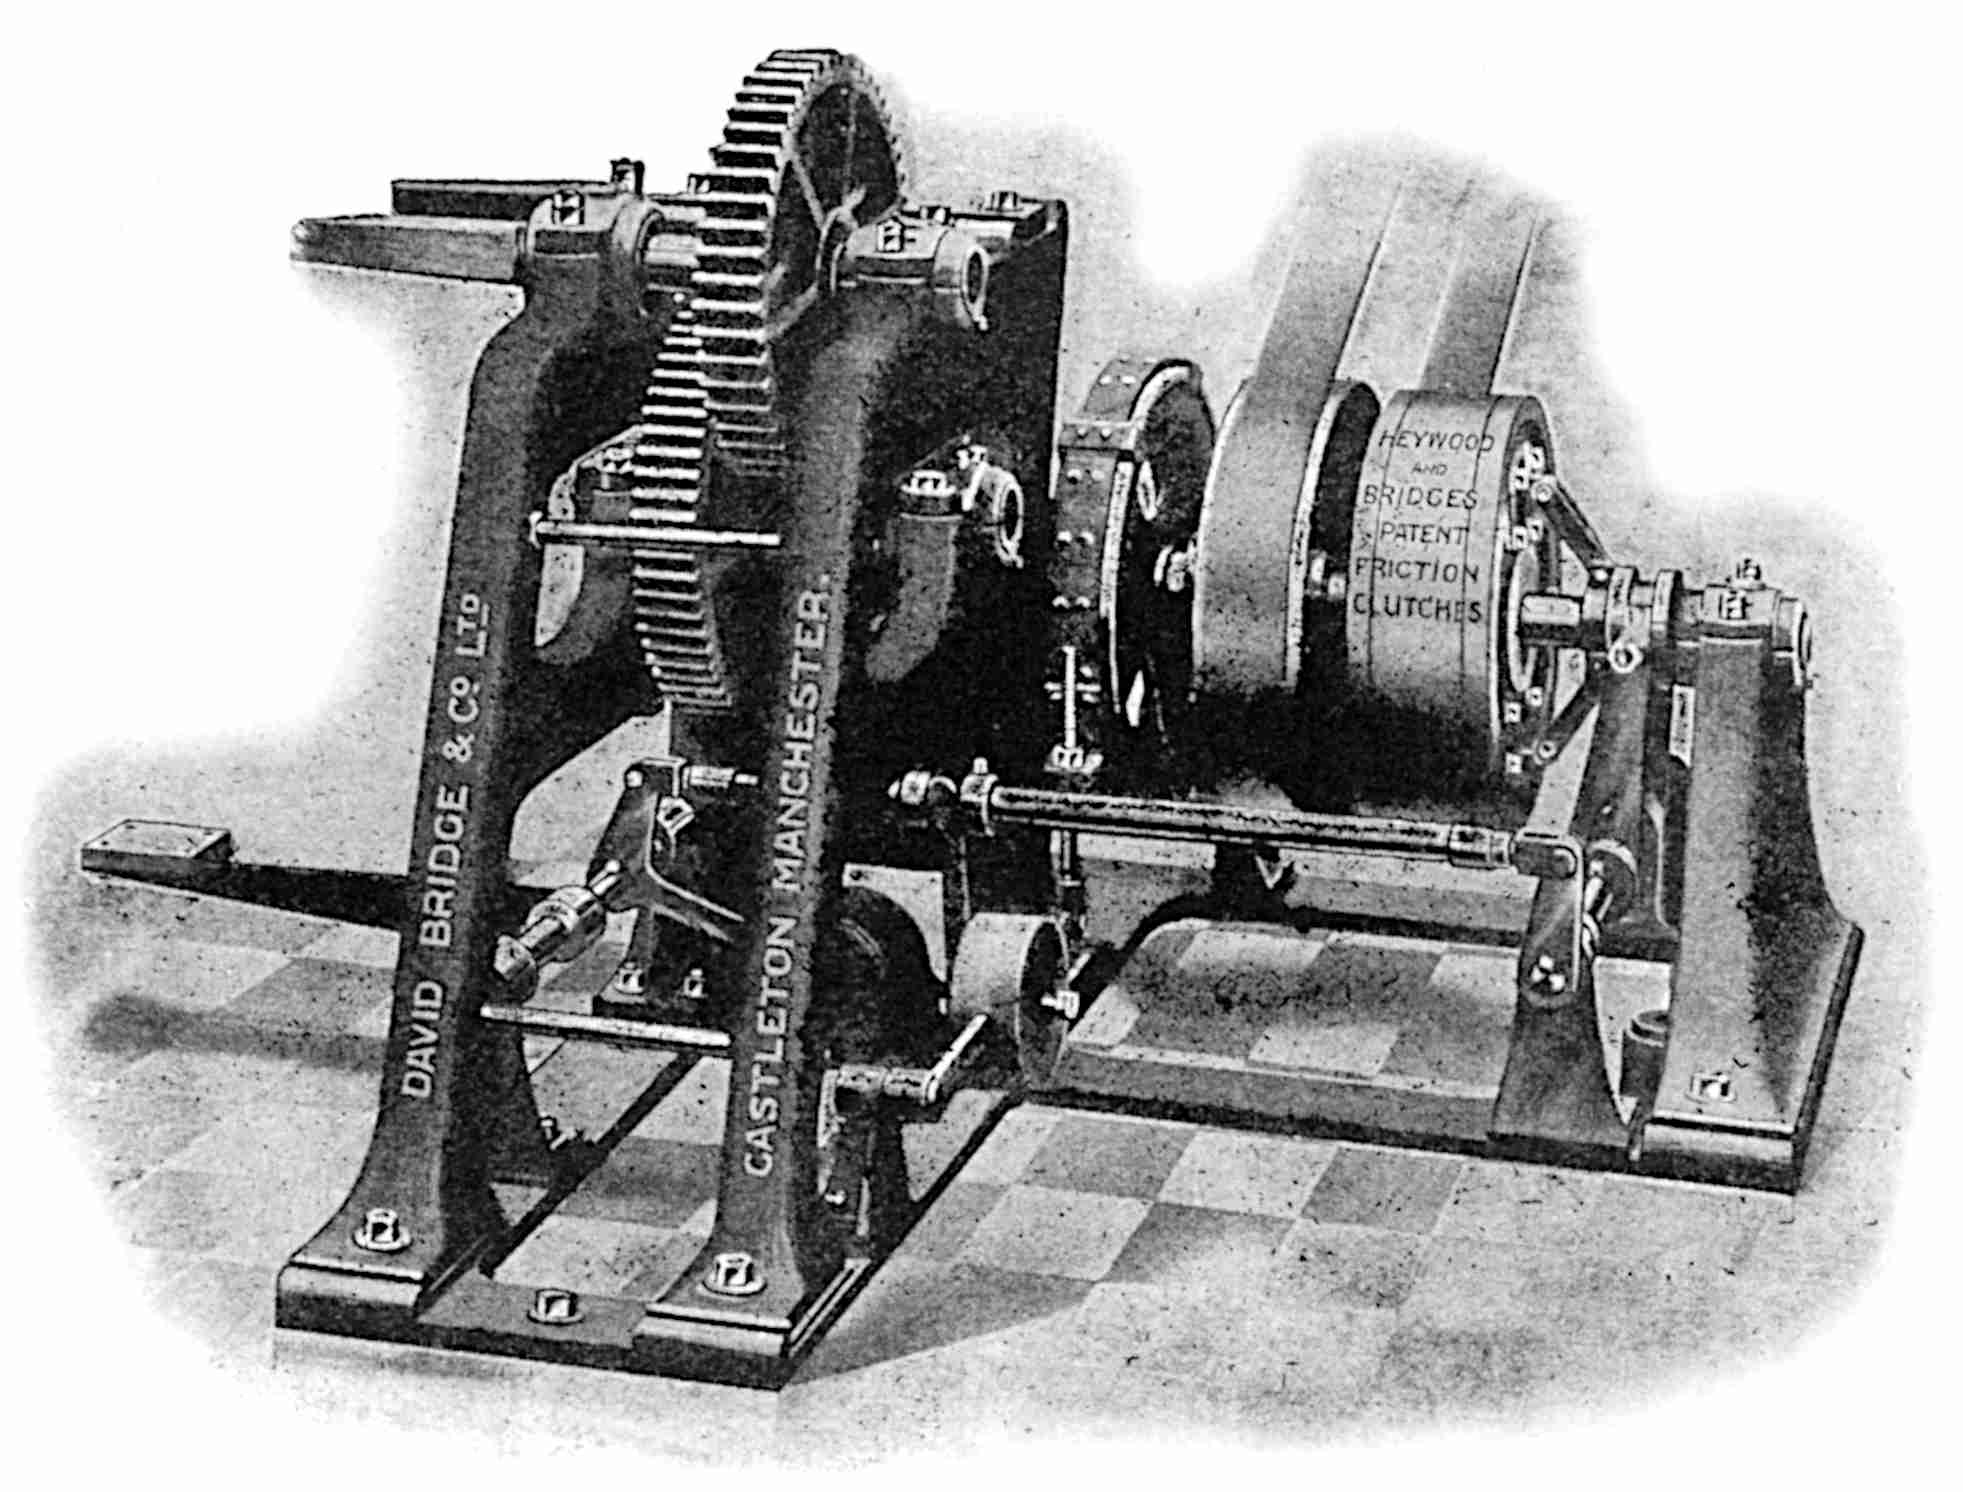
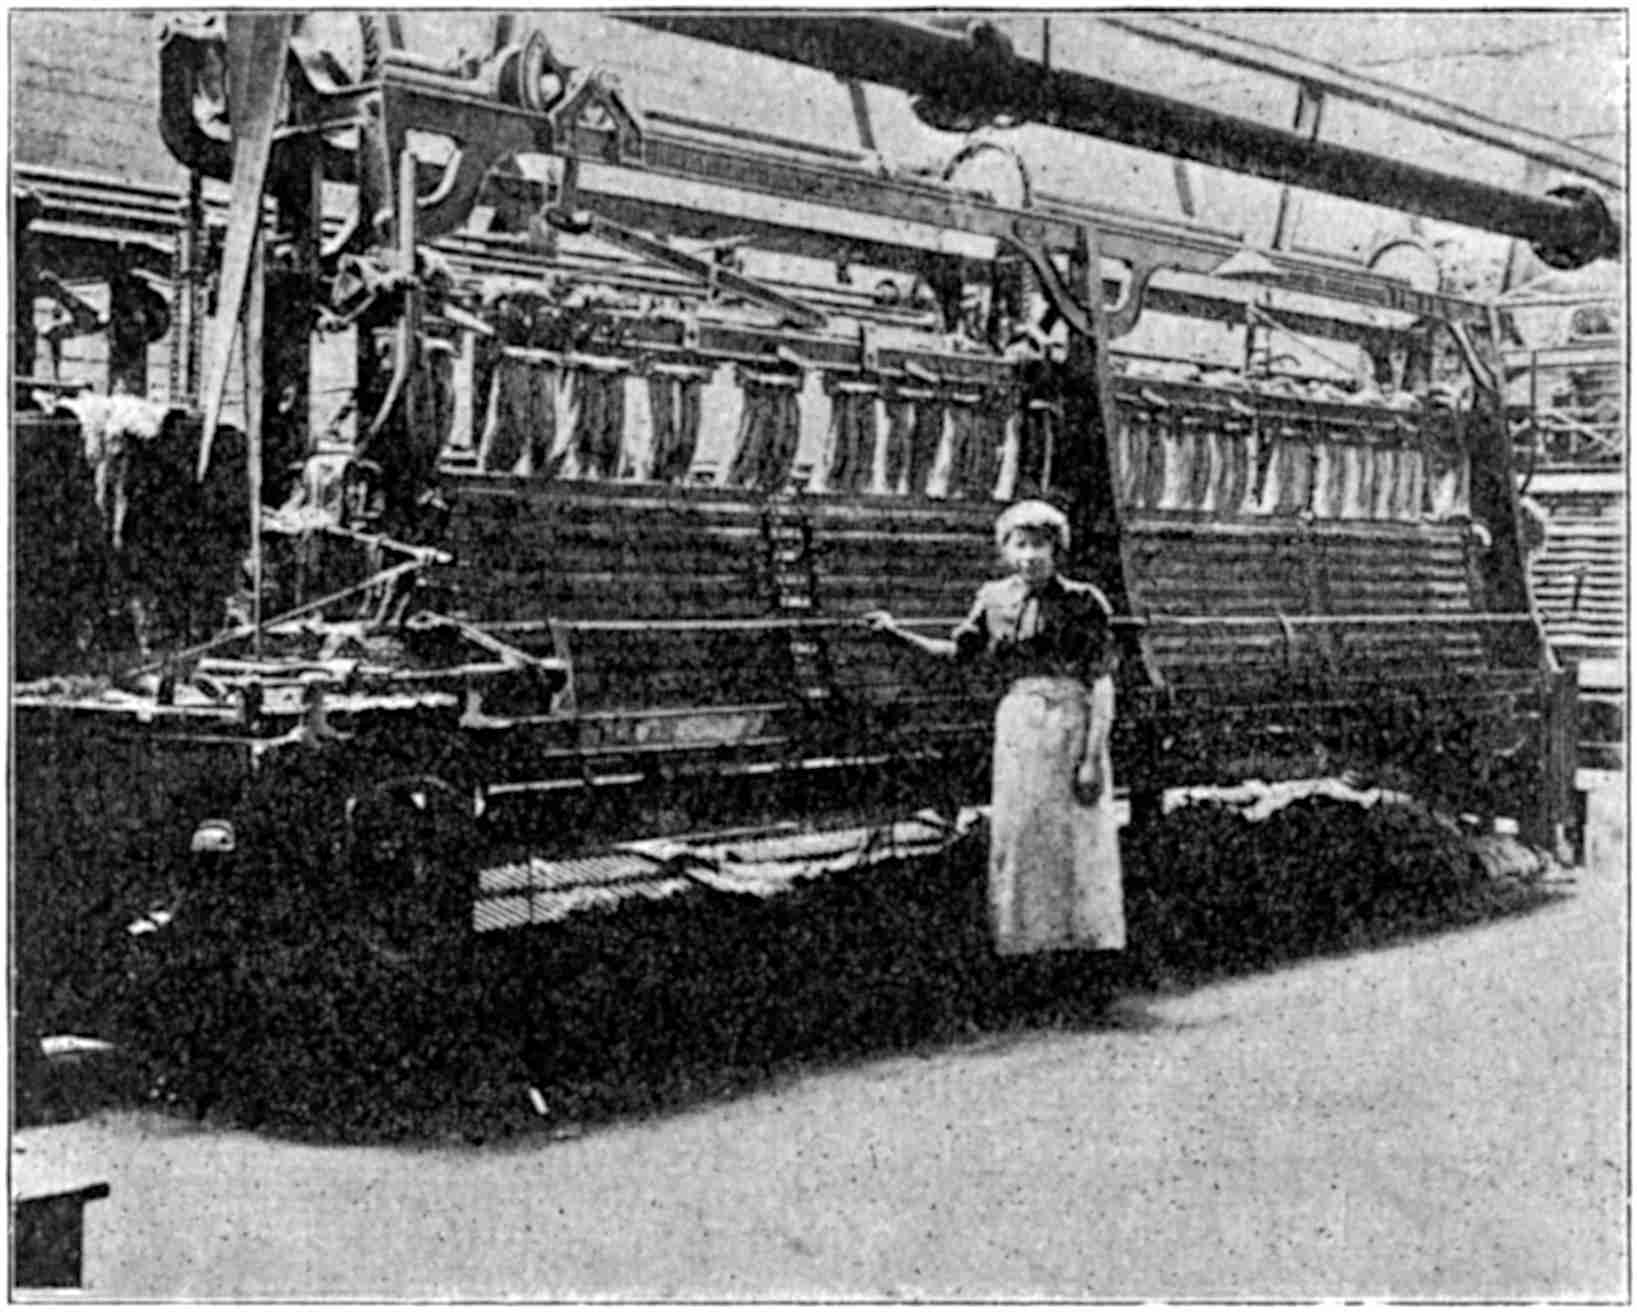
 . Most of these parts are clearly seen in