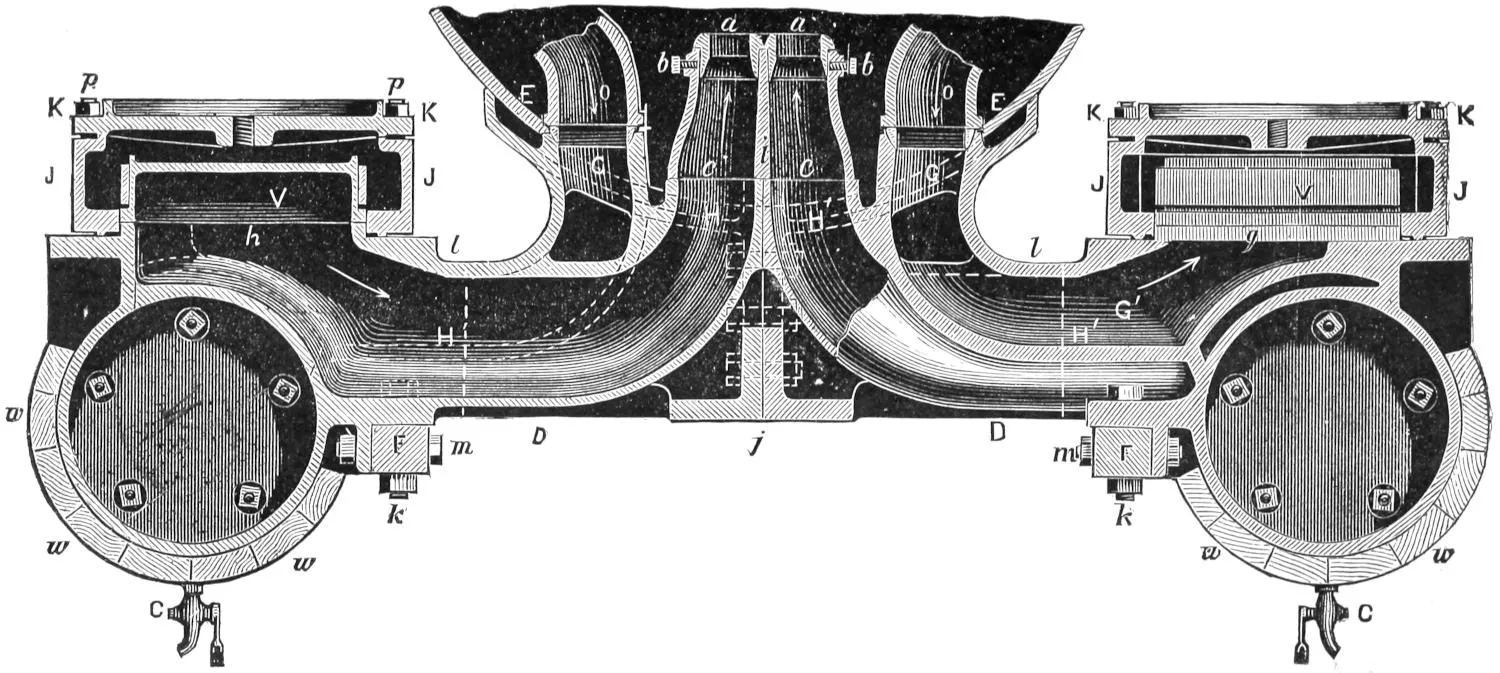
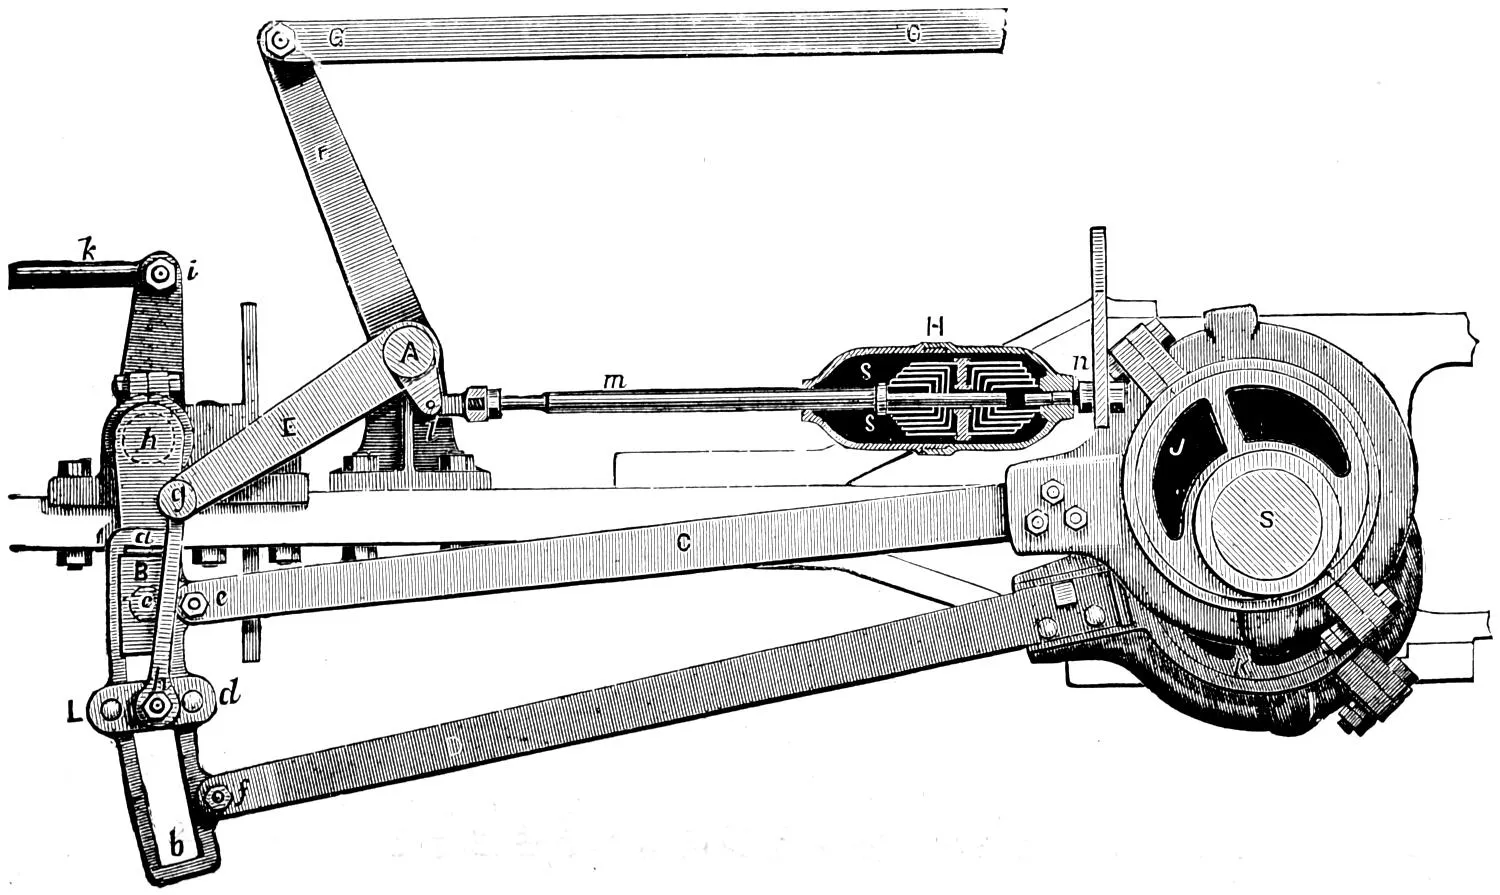
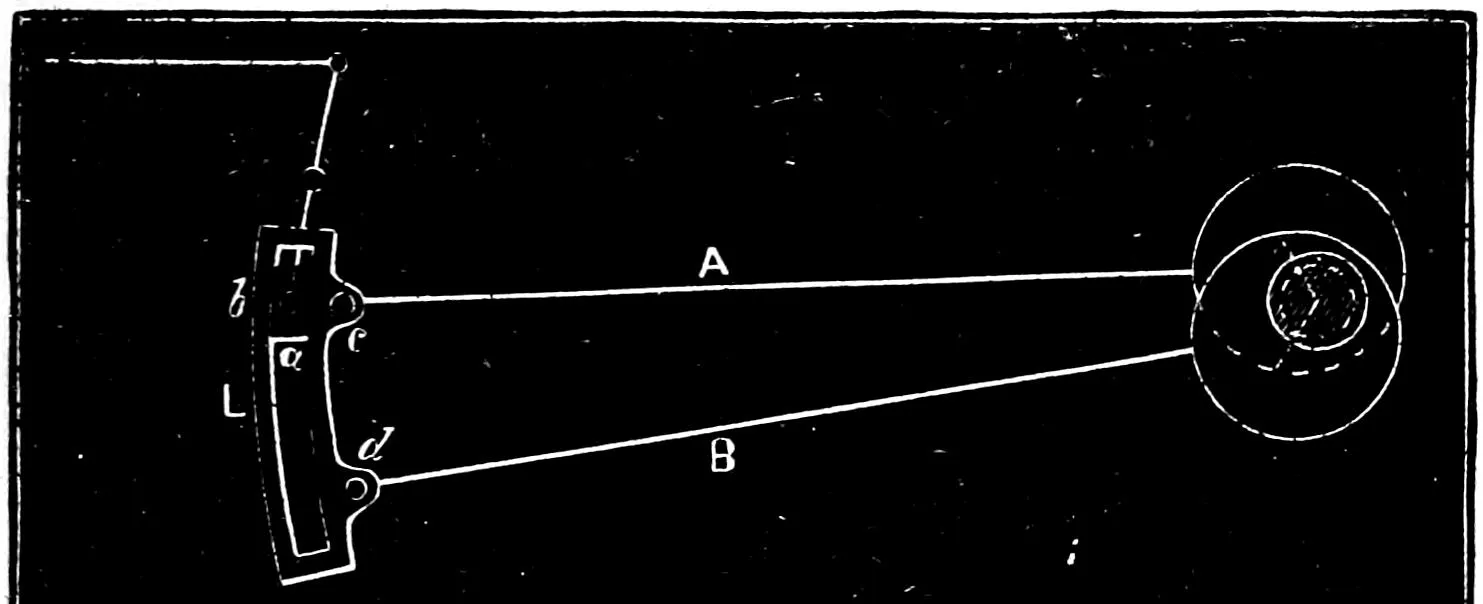
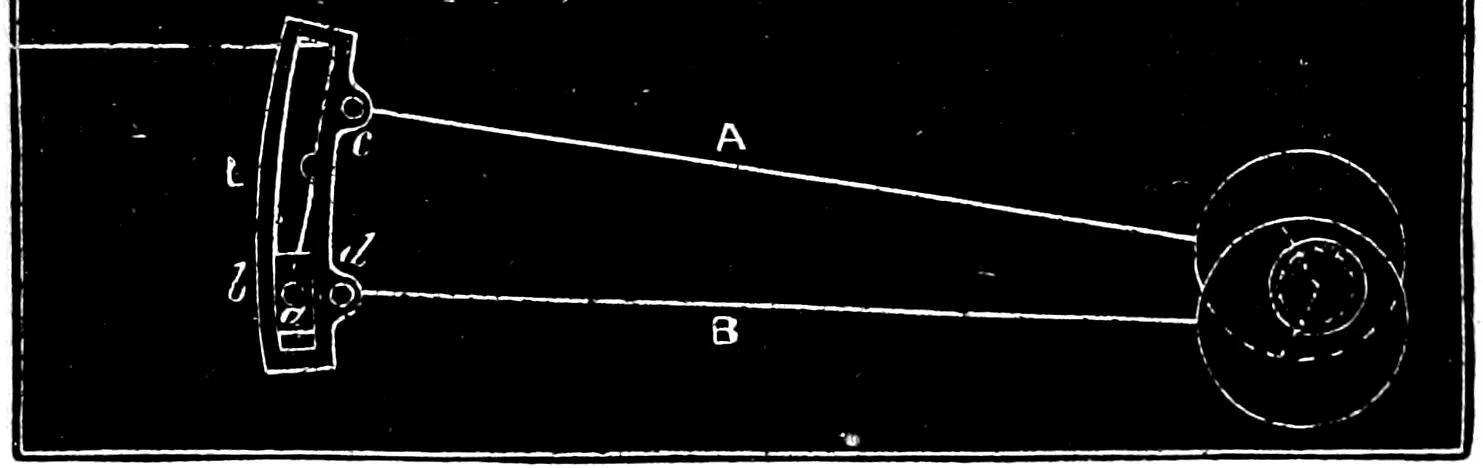
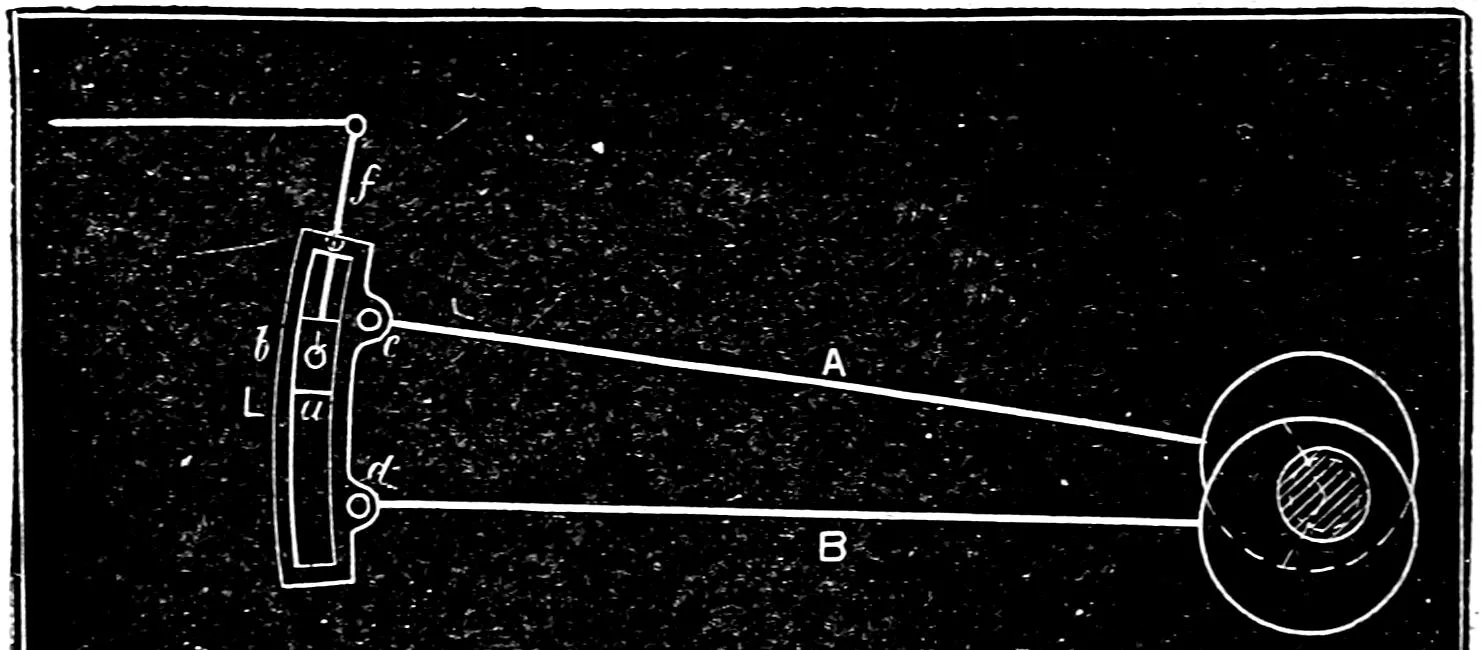
Most illustrations may be enlarged by clicking them
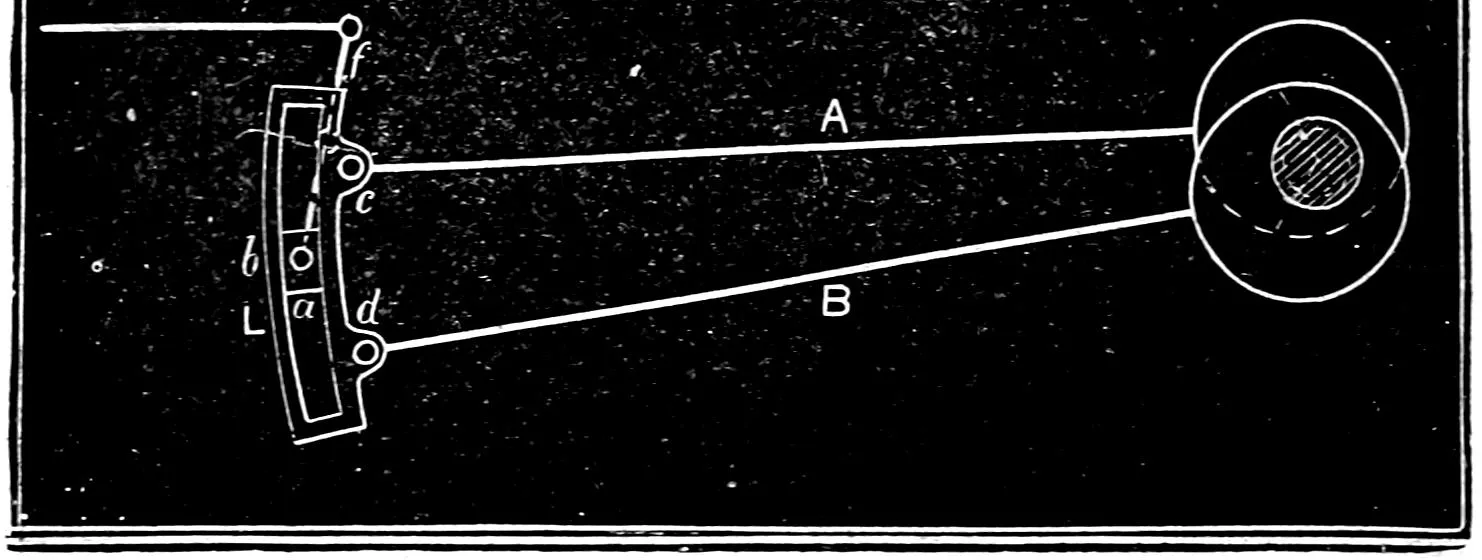
or by opening them in a new window or tab.
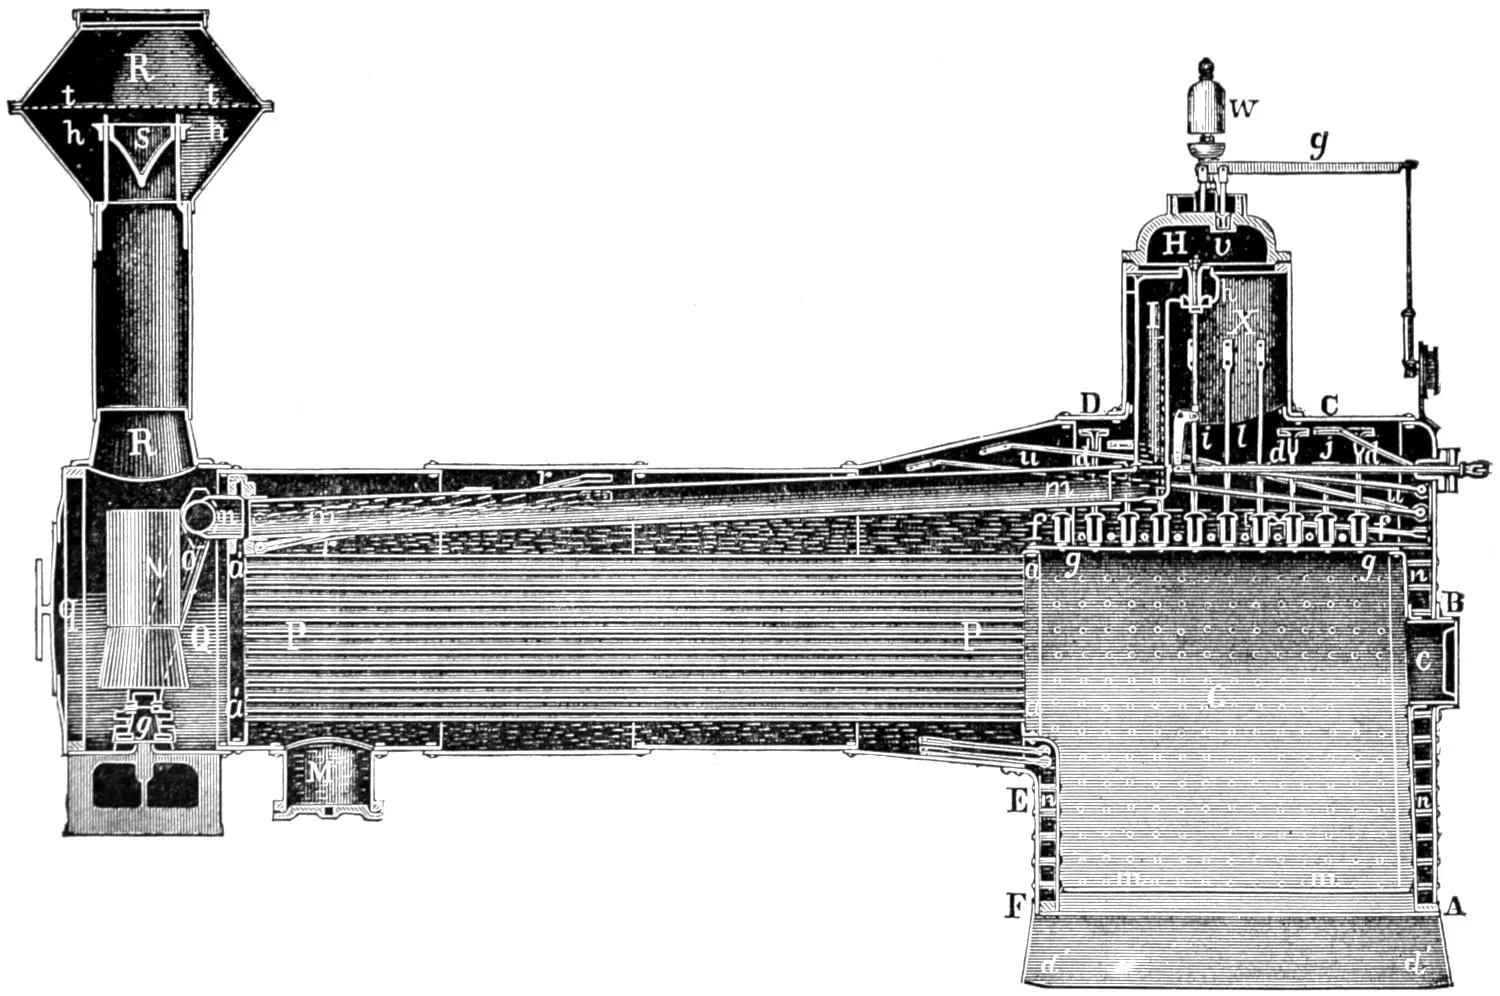
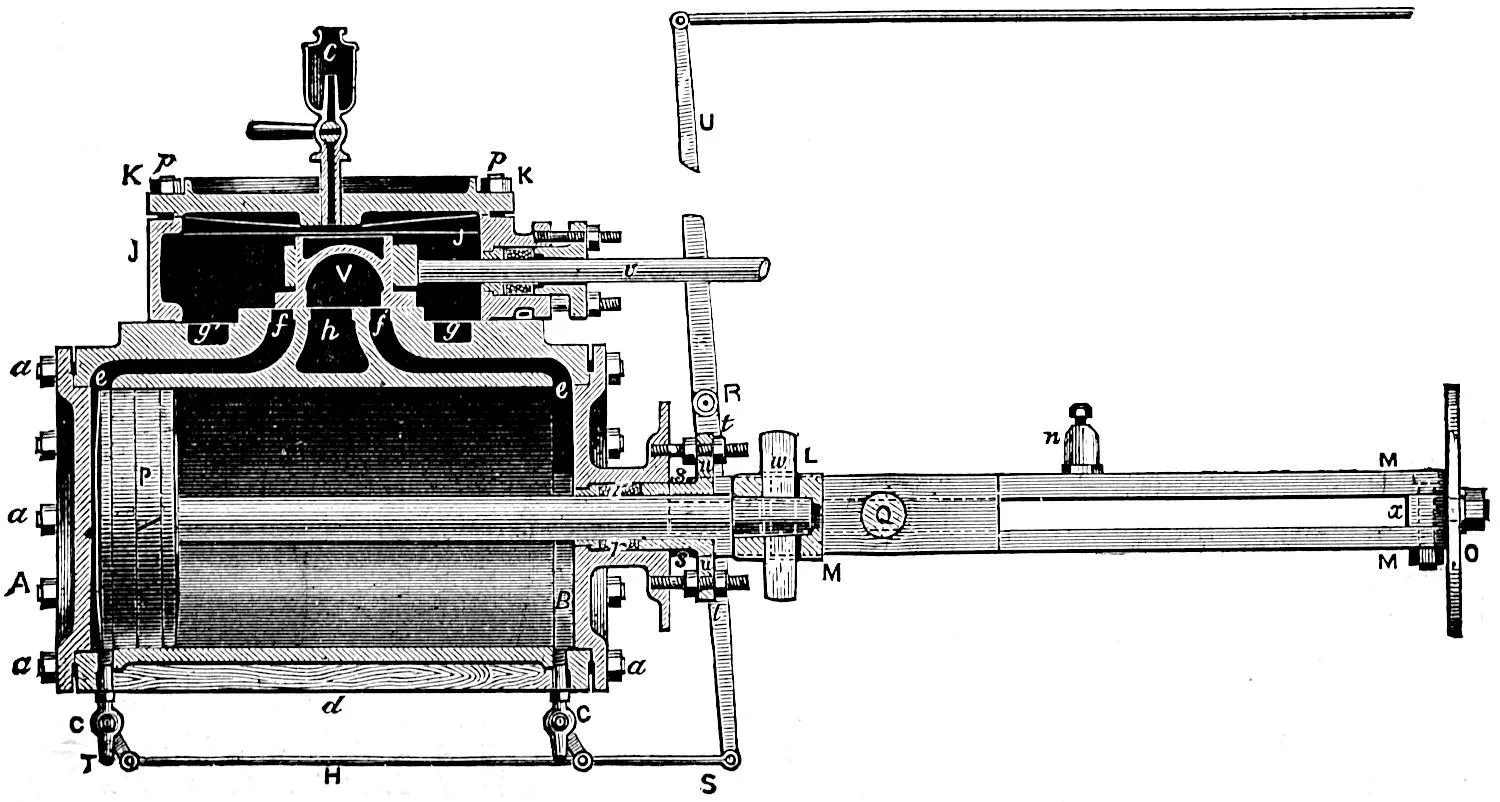
Plate II.
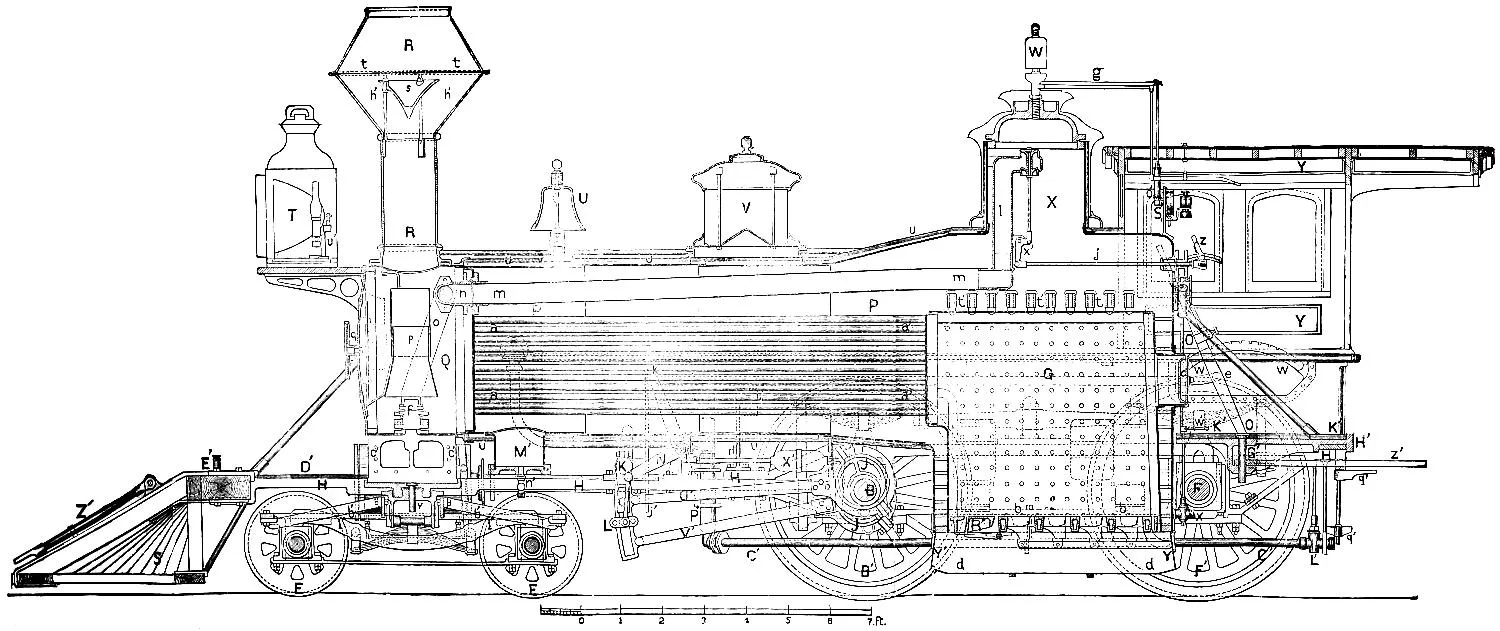
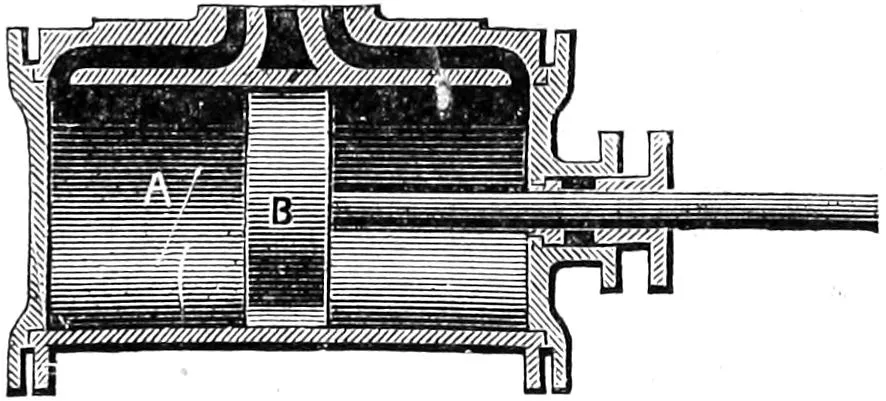
LONGITUDINAL SECTION OF AMERICAN LOCOMOTIVE. By The Grant Locomotive Works, Paterson, New Jersey. Scale, ³⁄₈ in. = 1 foot.
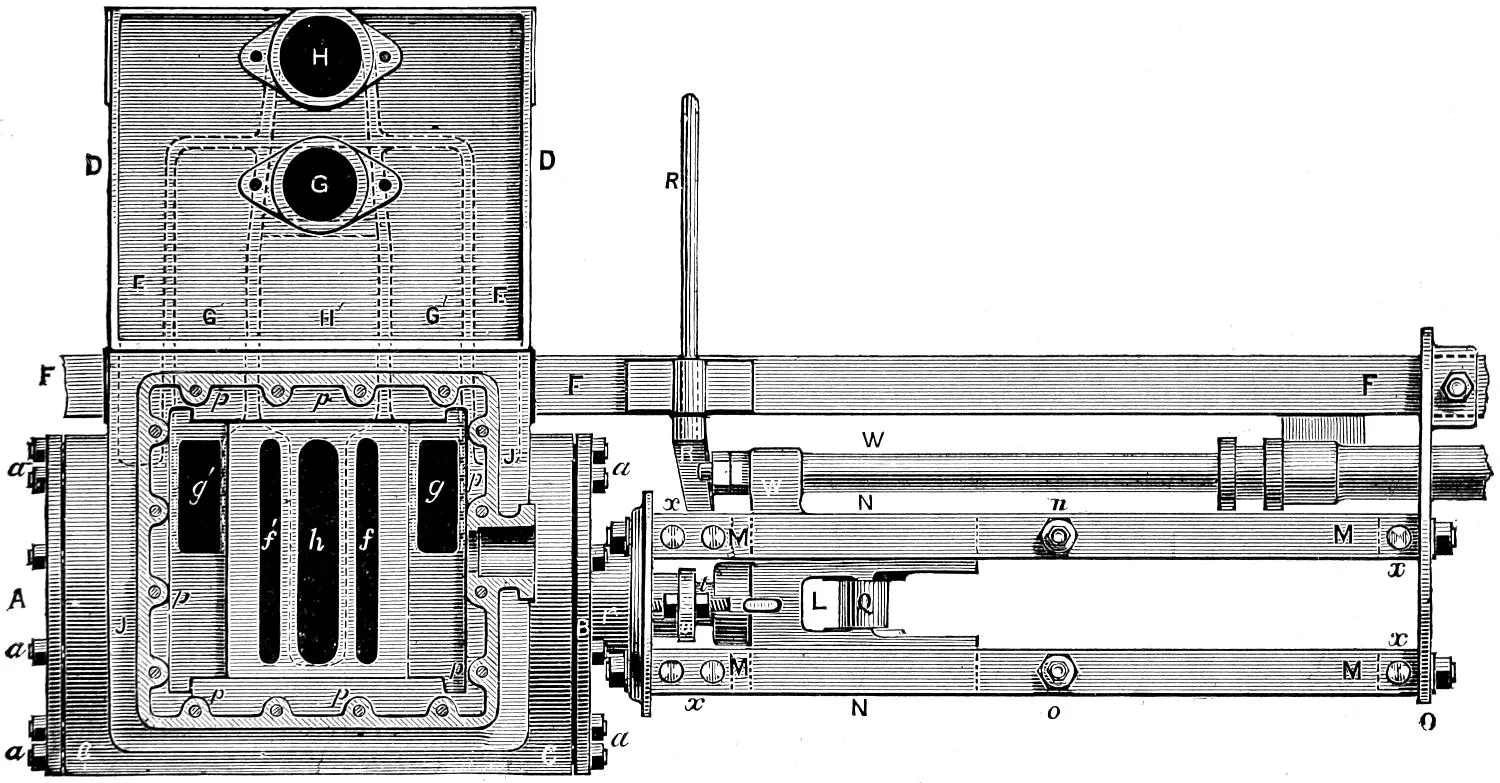
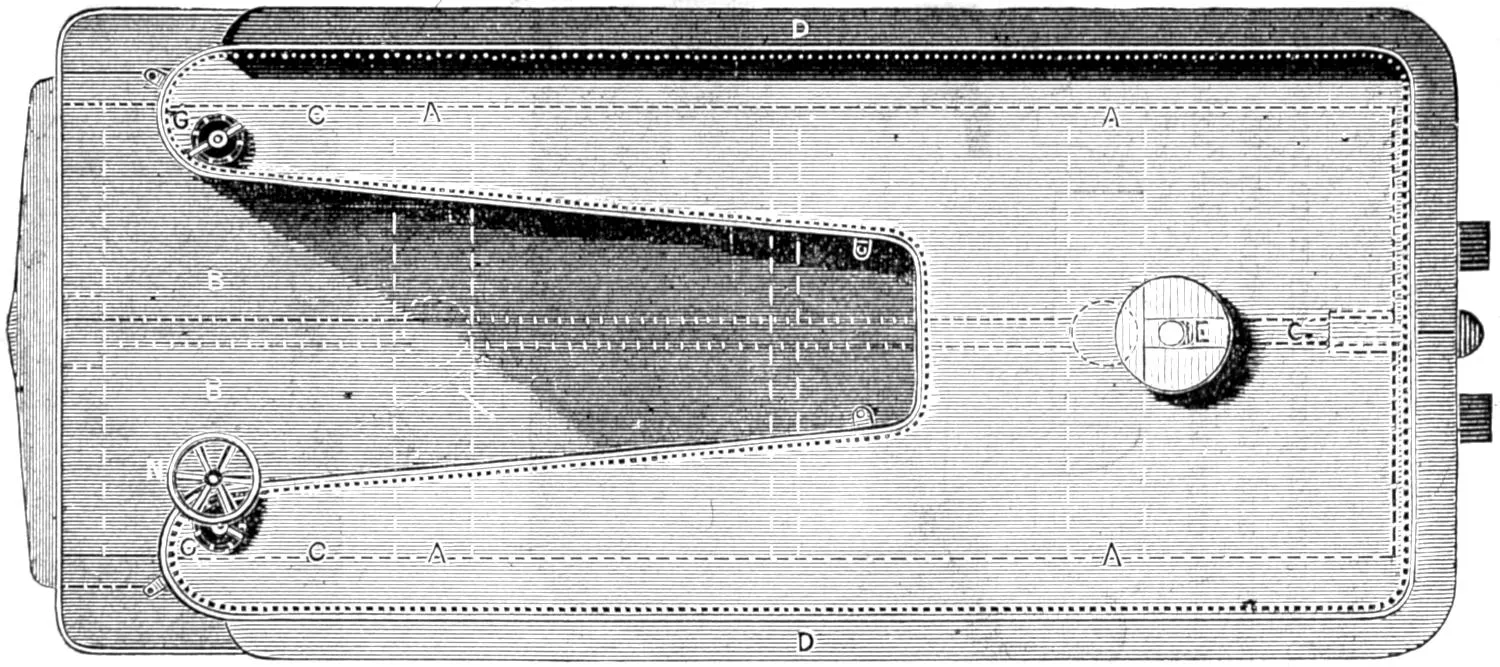
Plate III.
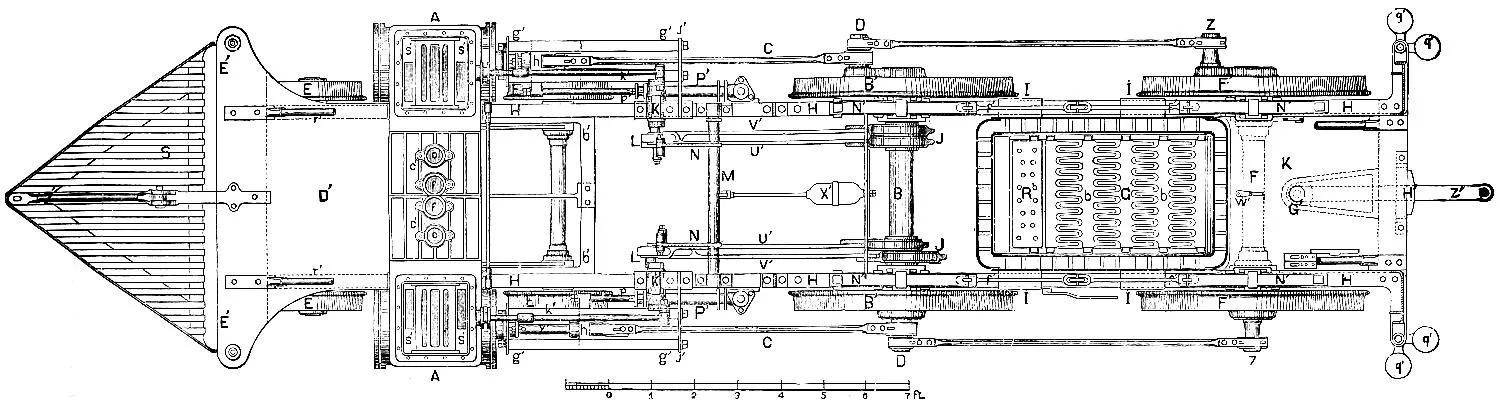
PLAN OF AMERICAN LOCOMOTIVE. By The Grant Locomotive Works, Paterson, New Jersey. Scale, ³⁄₈ in. = 1 foot.
BY MATTHIAS N. FORNEY, Mechanical Engineer.
Will be sent by mail, postage prepaid, on receipt of price $2.50.
FREDERICK KEPPY, Scientific Book Publisher,
No. 38 STATE STREET,
BRIDGEPORT, CONN.
Entered, according to Act of Congress, in the year 1874, by
THE RAILROAD GAZETTE,
In the office of the Librarian of Congress, at Washington.
PREFACE.
Books, like individuals, have their histories, and it
seems but proper that in introducing them somewhat
of their ancestry should be detailed. The present
book originated in this wise: the publishers of the
Railroad Gazette procured a copy of the “Katechismus
der Einrichtung und des Betriebes der Locomotive,”
by Georg Kosak. As no English translation
of this excellent little book was known to be in existence,
the editors of the above paper determined to
translate it and adapt it to the American practice in
the construction and management of locomotive steam
engines, and republish it in their journal. The translation
was therefore made and submitted to the writer
for revision and adaptation, according to the original
intention. Before the latter was entertained,
however, he had commenced writing an elementary
treatise on the locomotive. In revising the first part
of the translation of Mr. Kosak’s book, it was found
that the latter occupied only to a very limited extent
the ground which the writer had “staked out” in his
own incomplete plan. He therefore concluded to abandon
the original intention of “adapting” Mr. Kosak’s
work, and determined to rewrite it and make substantially
a new book of it. For the “idea,” however, and
to some extent its plan, and for much valuable material,
the author must acknowledge his indebtedness to Mr.
Kosak. In some few cases the language of the translator
has been employed, in part or in whole, without
quotation marks, but with an acknowledgment in a
foot-note. A similar plan has also been pursued in
using some other books. This was done to avoid cutting
up paragraphs and sentences into fragmentary
parts with numerous quotation marks.
The following books have been consulted and used
in writing the Catechism of the Locomotive: Heat
considered as a Mode of Motion, by Prof. Tyndall;
The Conservation of Energy, by Balfour Stewart;
Railway Machinery, by D. K. Clark; Treatise on the
Locomotive Engine, by Zerah Colburn; Treatise on
the Steam Engine, by W. J. M. Rankine; Indicator
Experiments on Locomotives, by Professor Bauschinger;
Richards’ Steam Indicator, by Charles T. Porter;
Die Schule des Locomotivführers, by J. Brosius and
R. Koch; Mechanics, by A. Morin; The New Chemistry,
by J. P. Cooke, Jr.; Combustion of Coal and the
Prevention of Smoke, by C. Wye Williams; A Treatise
on Steam Boilers, by Robert Wilson; Reports of
the American Railway Master Mechanics’ Association;
Link Valve Motion, by William S. Auchincloss, and
Emergencies and How to Treat Them, by Dr. Joseph
W. Howe.
For the title of the book an apology is perhaps
needed, as the word Catechism is associated in nearly
all persons’ minds we will trust with early religious and
theological instruction, and therefore a Catechism of
the Locomotive is very apt to sound more ludicrous
than scientific. The title of Mr. Kosak’s book was
adopted before it was determined to rewrite it, and it
was afterwards not deemed best to change it. To
those who are disposed to smile at it, the precedent of
Mr. Bourne’s excellent Catechism of the Steam Engine
is quoted, and if they will refer to Webster’s
Dictionary for the definition of the word “catechism,”
they will find that it means “an elementary book
containing a summary of principles in any science
or art, but appropriately in religion, reduced to the
form of questions and answers, and sometimes with
notes, explanations and reference to authorities,”
which is exactly what the present book is intended
to be.
To persons accustomed to books and study, the
catechetical form is very apt to seem cumbrous and
awkward, but it has some very decided advantages in
writing for those who have not acquired studious habits
of thought. To such the question asked presents first
a distinct image of the subject to be considered, so that
the explanation or instruction which follows is much
more apt to be understood than it would be if no such
question had been asked.
The author is indebted to Mr. D. B. Grant for the
use of drawings from which most of the engravings of
details of locomotives with which this book is illustrated
have been made, and to other locomotive builders,
whose engines are illustrated in the full-page
plates, for the drawings thereof. He has also received
very valuable aid from Mr. Richard H. Buel, Mechanical
Engineer; Mr. William Buchanan, Master Mechanic
of the Hudson River Railroad; Mr. Frank D.
Child, Superintendent of the Hinkley Locomotive
Works; and Mr. E. T. Jeffrey, Assistant Superintendent
of Machinery of the Illinois Central Railroad.
The object in writing the book was to furnish a
clear and easily understood description of the principles,
construction and operation of the locomotive engine
of the present day, a subject which is not concisely
or adequately treated in any one similar book.
If the author has succeeded in making what he has
written plain to plain people, his aim will be fully accomplished.
The Catechism of the Locomotive is intended for
a large class of readers, among whom are all kinds of
railroad officers and employes, consisting of locomotive
runners, firemen, and the many different kinds
of mechanics employed in railroad shops and in the
construction of locomotive and other kinds of railroad
machinery and material. Besides these there are
many amateur engineers, students, and persons interested
directly or indirectly in railroads, and a not inconsiderable
class who are always seeking information
on all subjects whatsoever. It is evident, therefore,
that the only way to adapt the book to all the classes
for whom it is intended, was to make it so plain that
the “wayfaring man” will have no difficulty in comprehending
it. It has therefore been written in as
clear language as the writer could command, and the
subjects presented are treated as simply and as plainly
as his ability enabled him to do, and with the least
possible employment of either scientific or practical
technicalities. The only deviation from this plan will
be found in the use of algebraic symbols to designate
arithmetical calculations. This was done to save
space, and because it was thought that they could be
explained so that even those without any knowledge
whatsoever of algebra could easily comprehend them.
To such as have no such knowledge the following explanation
is given:
Suppose it is necessary to add two numbers, say
1,872 and 468. The calculation, if made arithmetically,
would be thus:
1,872
468 2,340
This it will be seen occupies the space of several lines
of print. If we want to express this calculation algebraically,
it can be done by simply writing the two
numbers and placing the sign +, called plus, between
the two, which indicates that they are to be added
together, thus:
1,872 + 468
To indicate what the sum will be, or what the two
added together will amount to, the sign =, called
equal to, or the sign of equality, is placed after the
two numbers and between them and the sum, thus:
1,872 + 468 = 2,340,
which can be read as follows:
1,872 added to 468 is equal to 2,340.
Now the only use of the algebraic signs + and = is
that they save time in writing and room in printing,
and when persons become accustomed to their use they
make plain a number of operations at a single glance,
as will be shown hereafter.
In the same way that the sign + means added to,
the sign - means less or subtracted from, thus:
1,872 - 468 = 1,404,
which is the same as though it was printed as follows:
1,872 less 468 is equal to 1,404.
The sign × means multiplied by, or is the sign of
multiplication. Thus:
1,872 × 468 = 876,096;
that is,
1,872 multiplied by 468 is equal to 876,096.
The sign ÷ means divided by, thus:
1,872 ÷ 468 = 4.
which means:
1,872 divided by 468 is equal to 4.
The same thing is expressed by putting a line
under the dividend and writing the divisor under the
line, thus:
1,872468
= 4.
These signs are combined in various ways. Thus,
supposing we wanted to add 1,872 to 468 and then
divide the sum by 117, it would be necessary, in order
to represent the arithmetical calculation, to do it as
follows:
1872
468
117)2340(20 234
0
Algebraically it would be stated thus:
1872 + 468117
= 20
If you wanted to add 124 to the quotient 20 above,
the calculation would be as follows:
1872 468
117)2340( 20 234 124
0 144
This operation could be expressed by writing it as
follows:
1872 + 468117
+ 124 = 144.
If we wanted to multiply the quotient 20 by 124
we would simply put the sign × instead of + before
124, thus:
1872 + 468117
× 124 = 2480.
The sign of subtraction or division can be used in
the same way.
With these explanations it is believed that any one,
with nothing more than an ordinary knowledge of the
four elementary rules of arithmetic, can understand all
the mathematics contained in the following pages.
A little explanation may also be needed of the method
of representing machinery and other structures by
mechanical drawings.
A
B
C
D
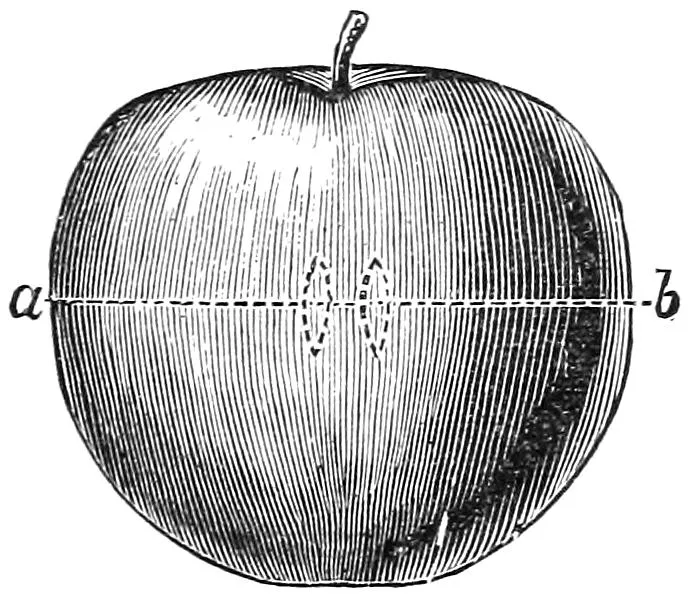
If we want to represent the outside of any object,
say an apple, we make a drawing of it as shown at A.
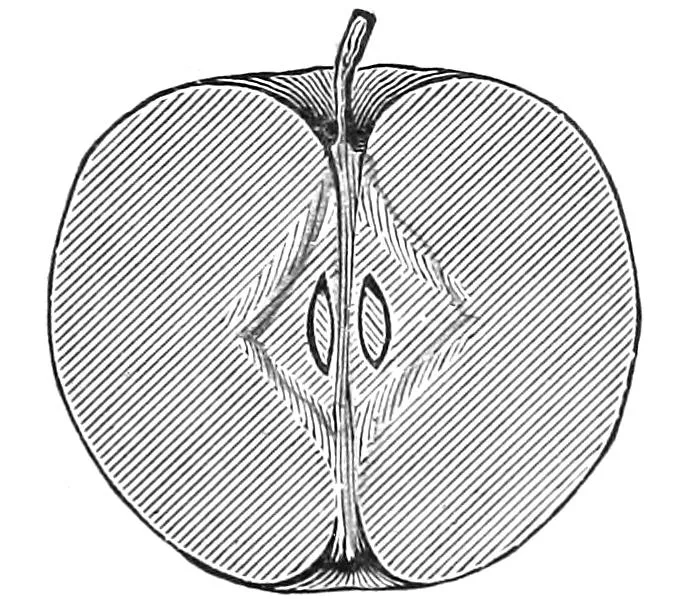
Now if we want to show the inside of the apple, say
the seeds and core, we can cut it in half and represent
it as shown at C, which is then called a section or sectional
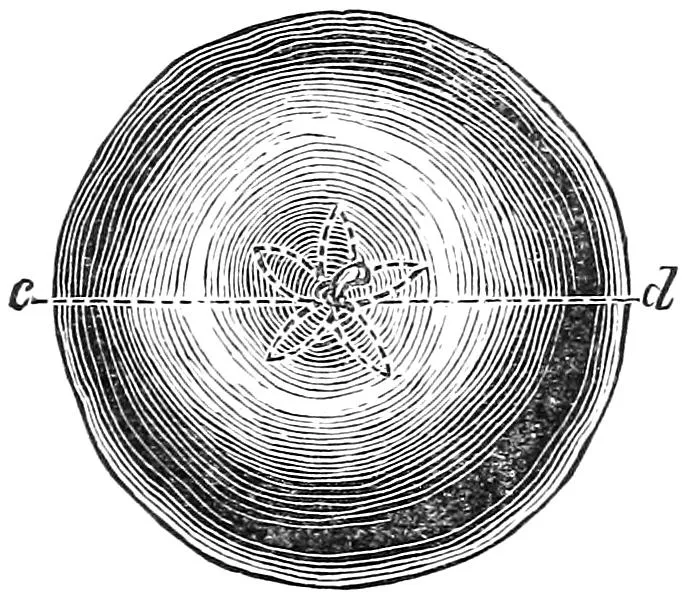
view of the apple. If we represent it as it will
appear if we are above it and looking down on it as
shown at B, it is called a top view or plan.
It is evident, too, that it might be desirable to show
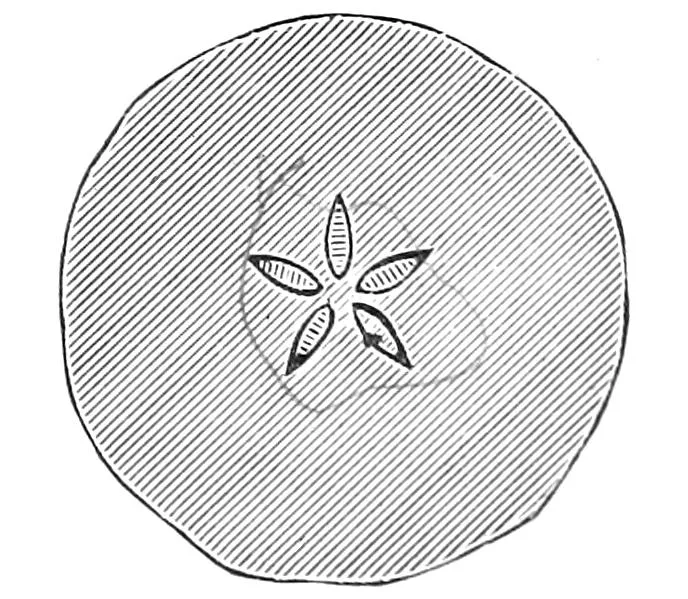
the arrangement of the seeds in the apple as they
would appear if it was cut through in the other direction,
say on the line a b, fig. A, and as is shown at D.
There are therefore two kinds of sections; one C, in
which the object is supposed to be cut through vertically,
and therefore called a vertical section, the other
when the object is supposed to be cut through horizontally,
and therefore called a horizontal section, as
shown at D.
It is also evident that in looking at a locomotive
or any other object, the appearance of the engine
depends upon our position in relation to it. Thus, if
we stand on the side of it, we see that part of
the engine, and a drawing which represents the side,
is therefore called a side view or side elevation. A
drawing which represents a locomotive or other
object as it would appear to us if we stood in
front of it, is called a front view or front elevation,
and a representation of the back part of any object
as it would appear to us if we stood behind it is
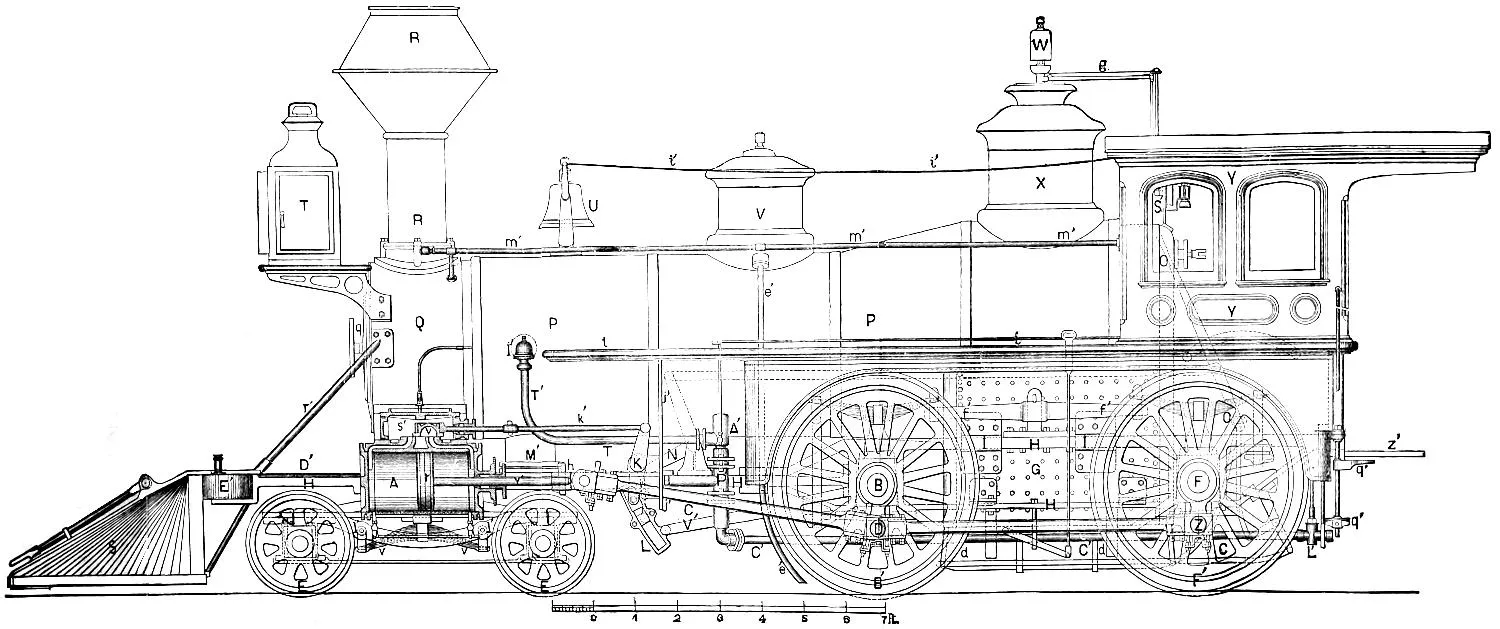
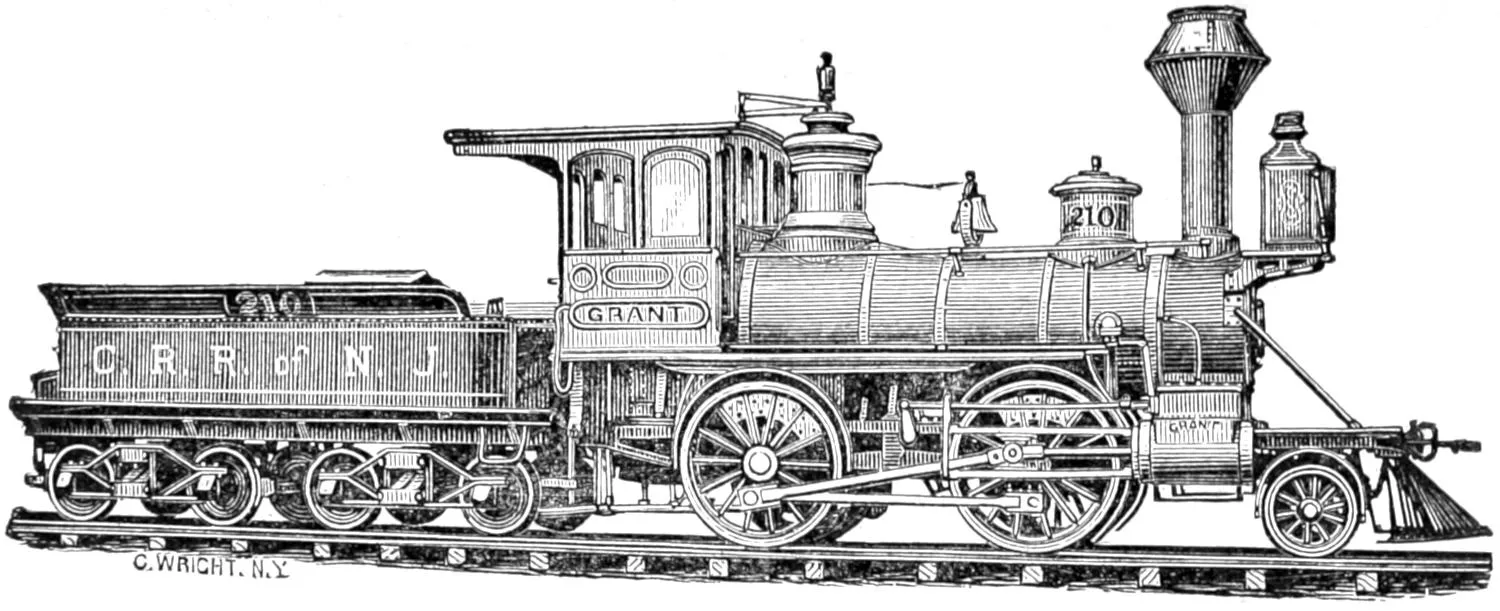
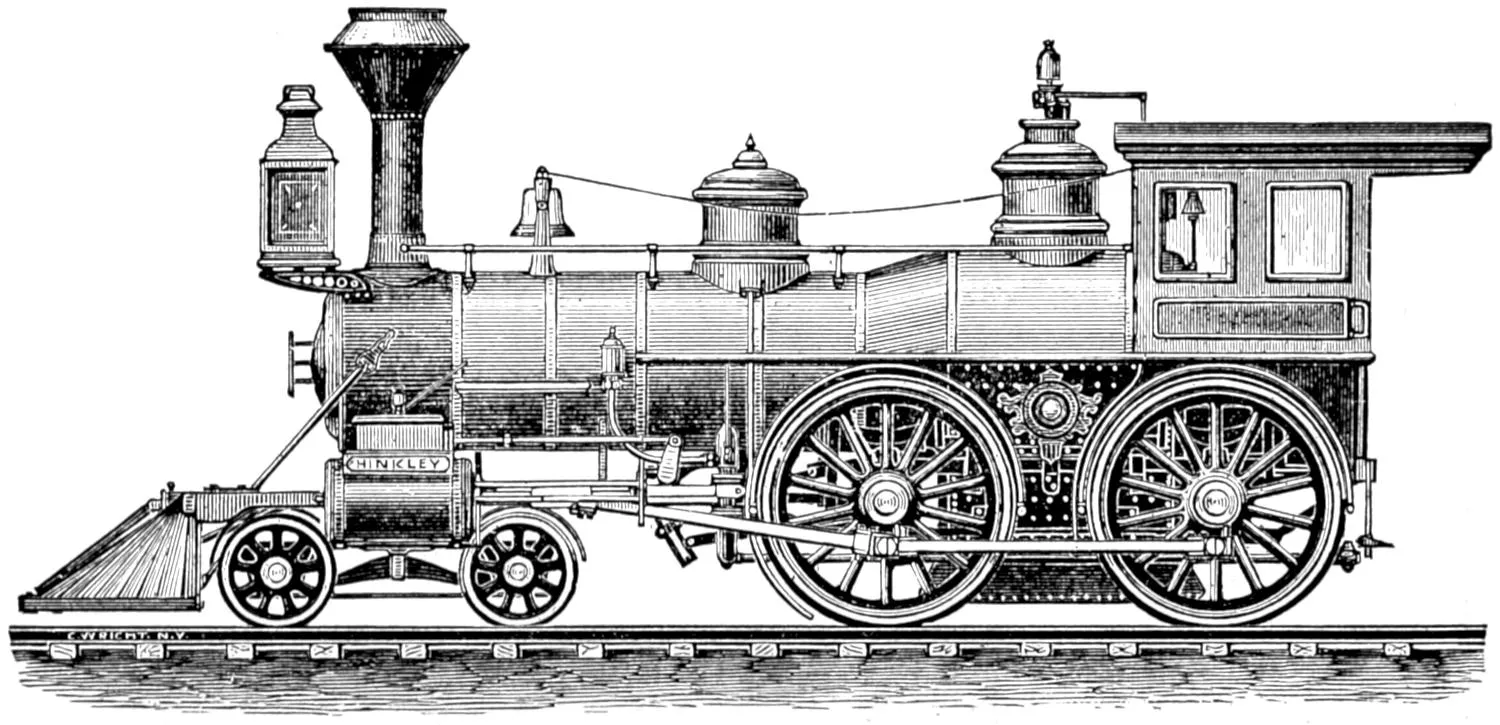
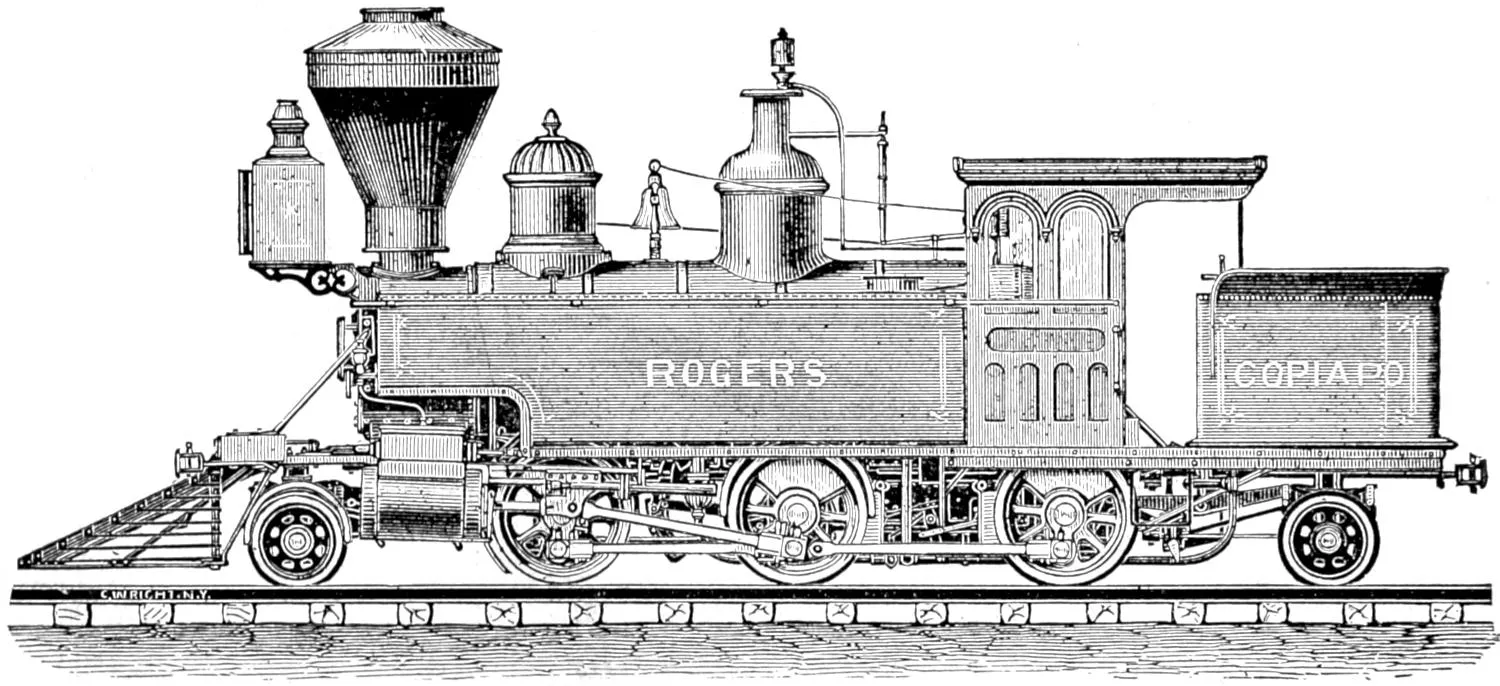
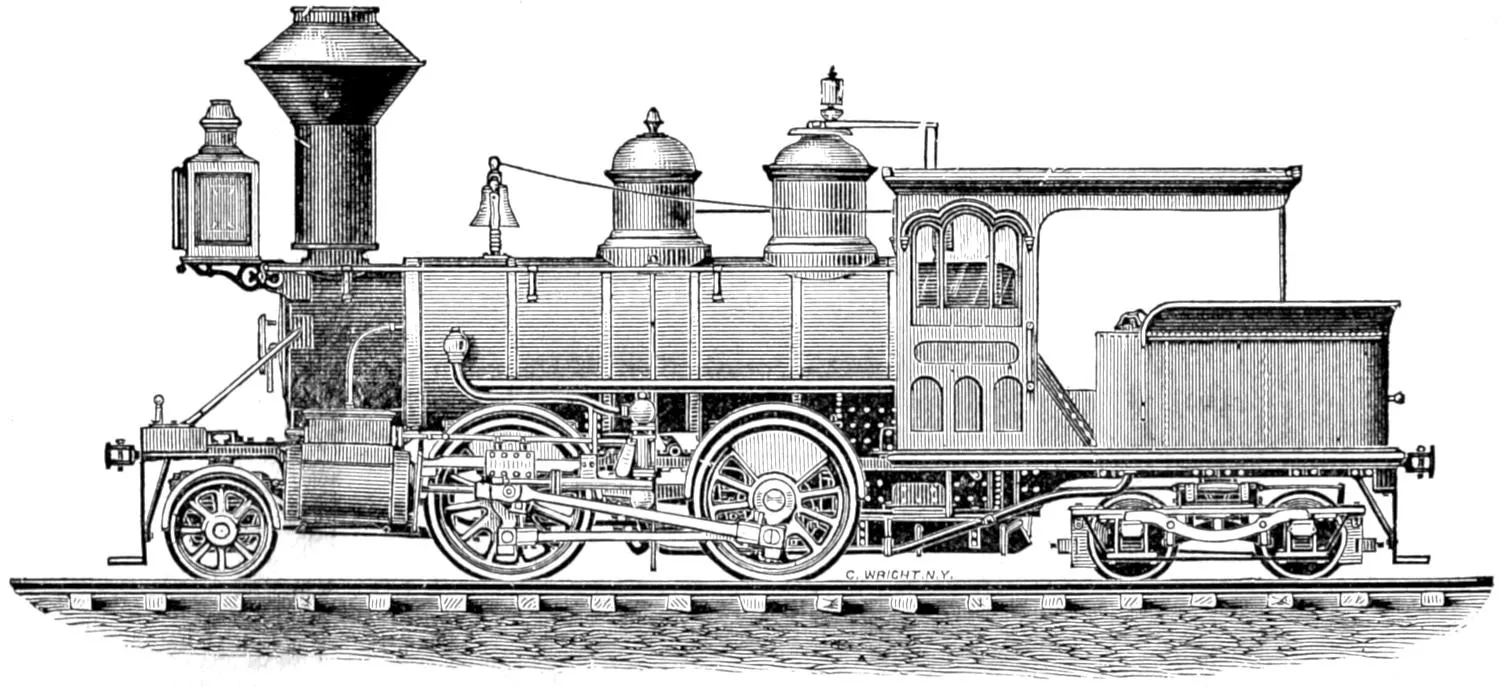
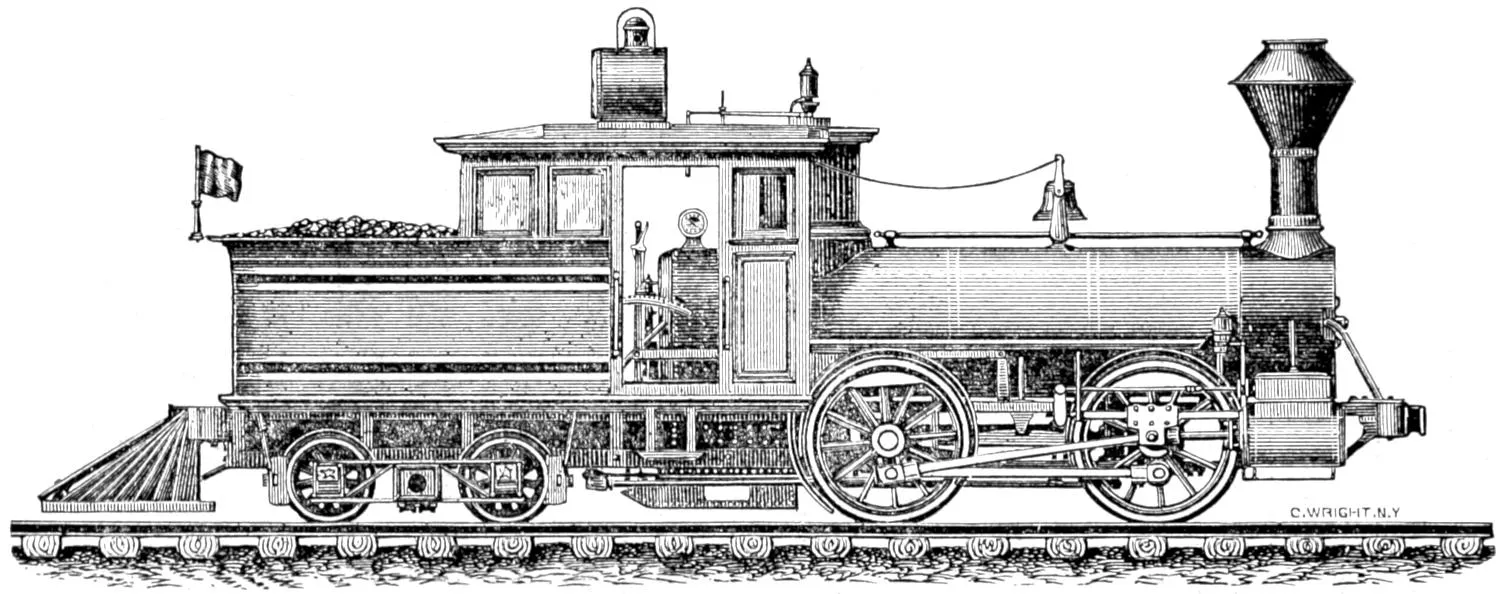
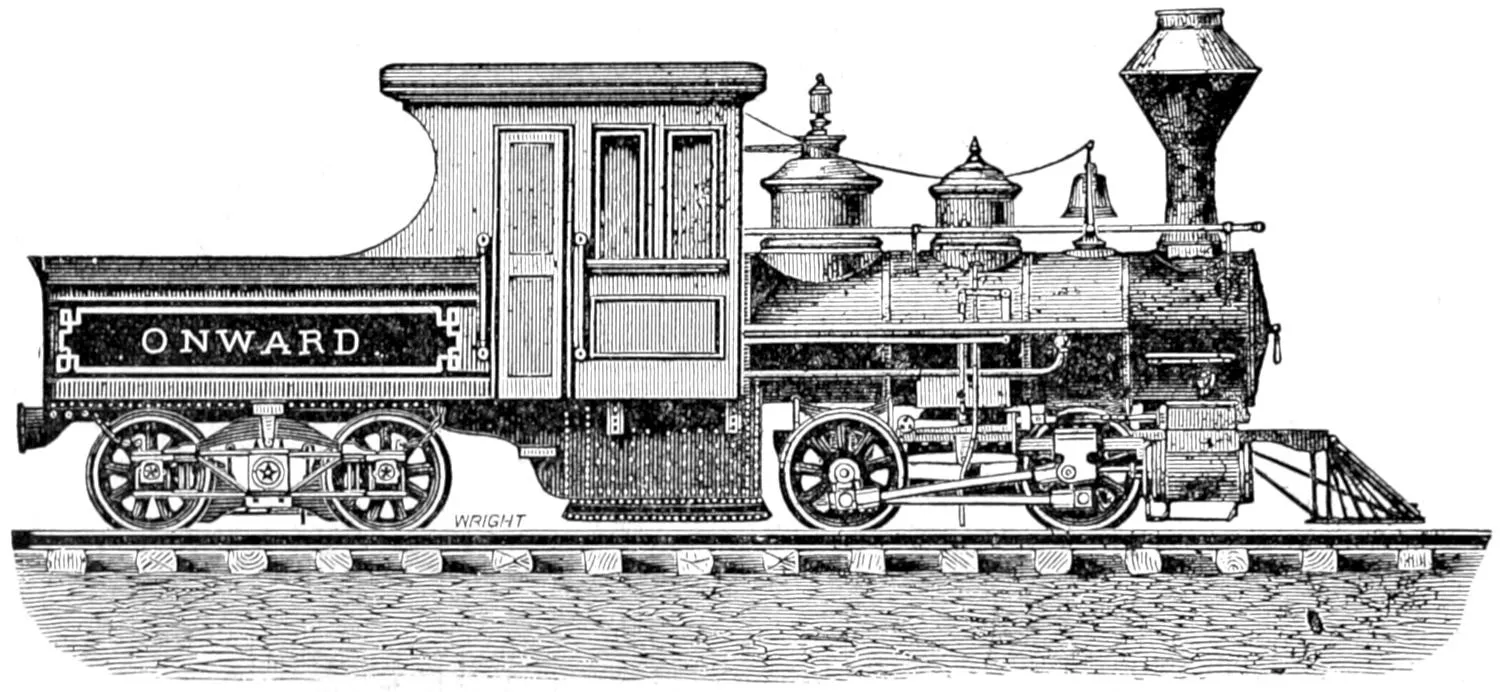
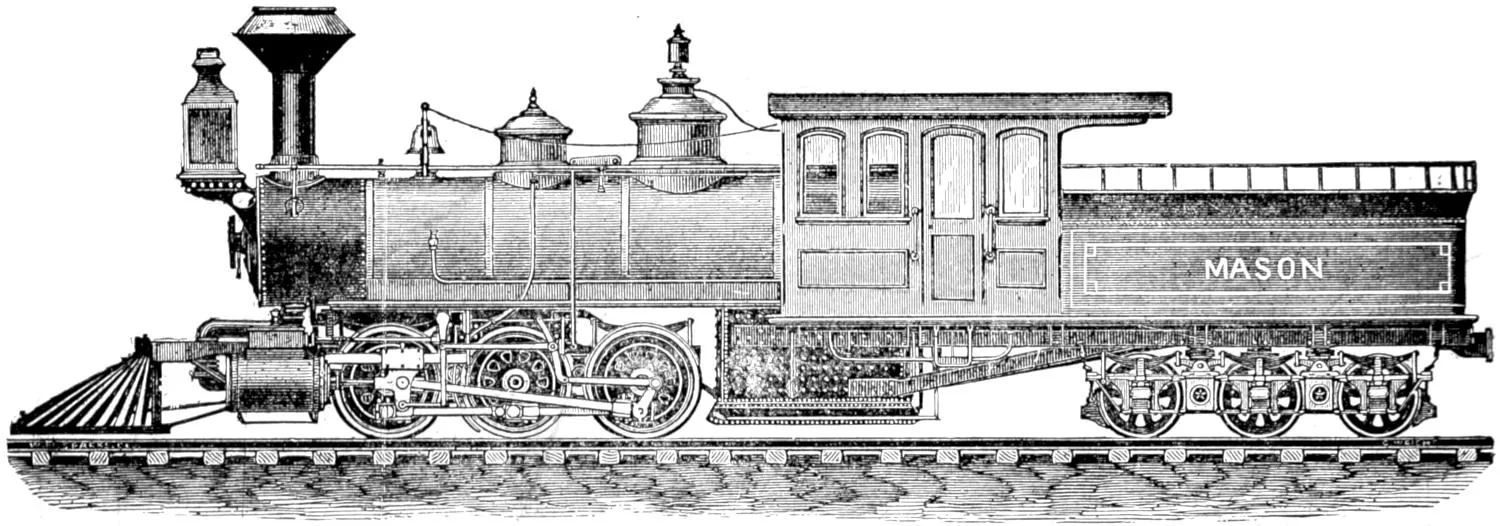
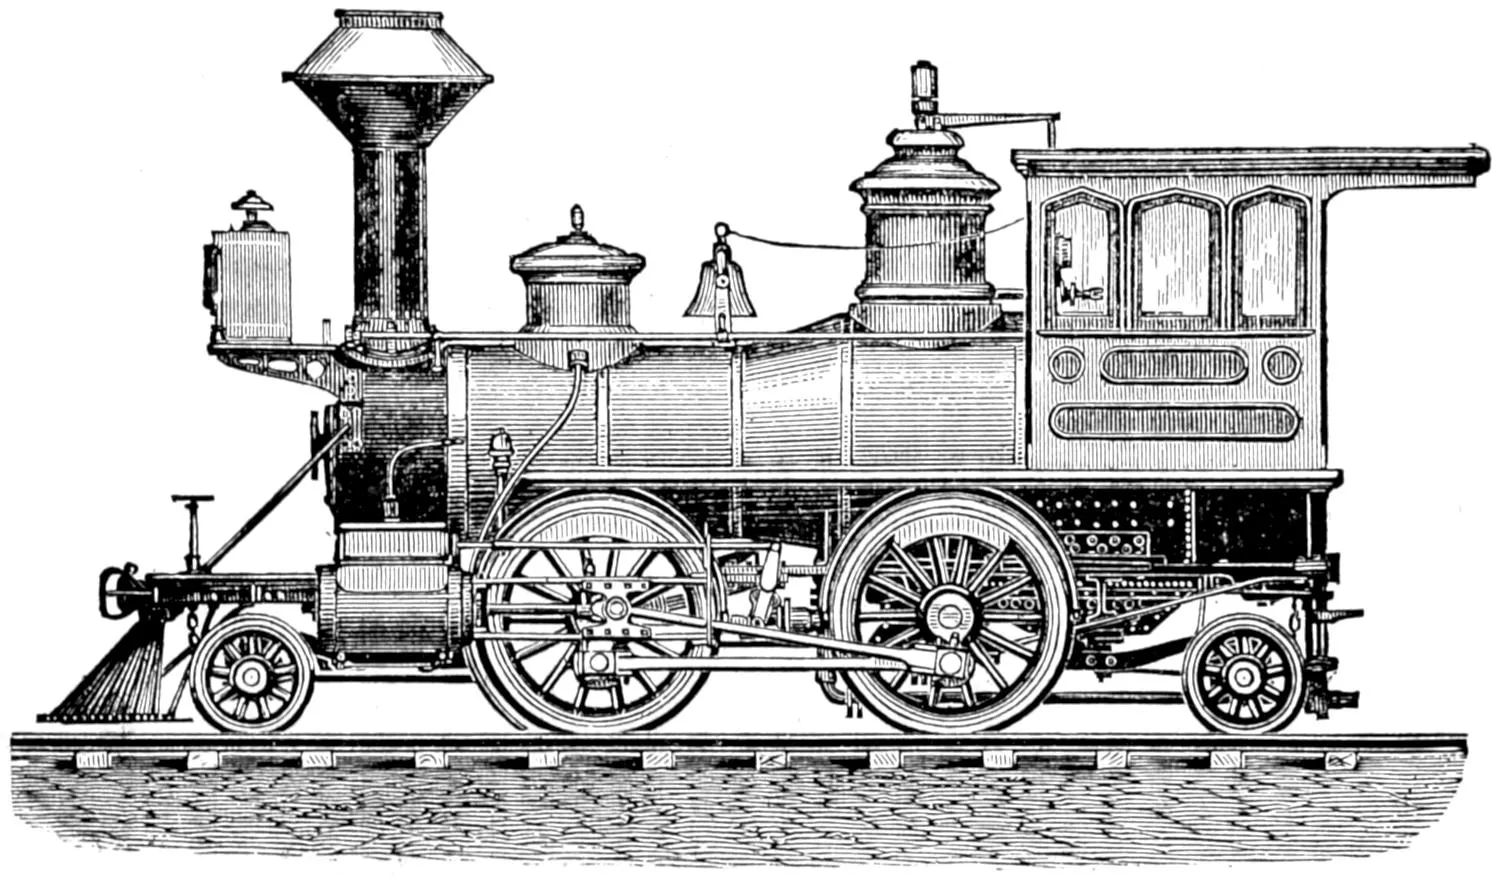
called a back view or back elevation. Plate I is a side
view, Plate II a section, Plate III a top view or
plan;[1]
the vignette in the title page is a front view and
fig. 71 a back view of a locomotive. If the drawing
is made as the object would appear if it was turned
upside down, and we were looking at it from above,
then it is called an inverted plan.
[1] The boiler of the locomotive is supposed to be
removed in Plate III.
It is obvious, too, that it is possible to make a great
many different sectional views of nearly any object,
especially of a machine. Thus, we could suppose a
locomotive cut through vertically and lengthwise, as is
shown in Plate II. Such a representation is called a
longitudinal section. A locomotive could also be cut
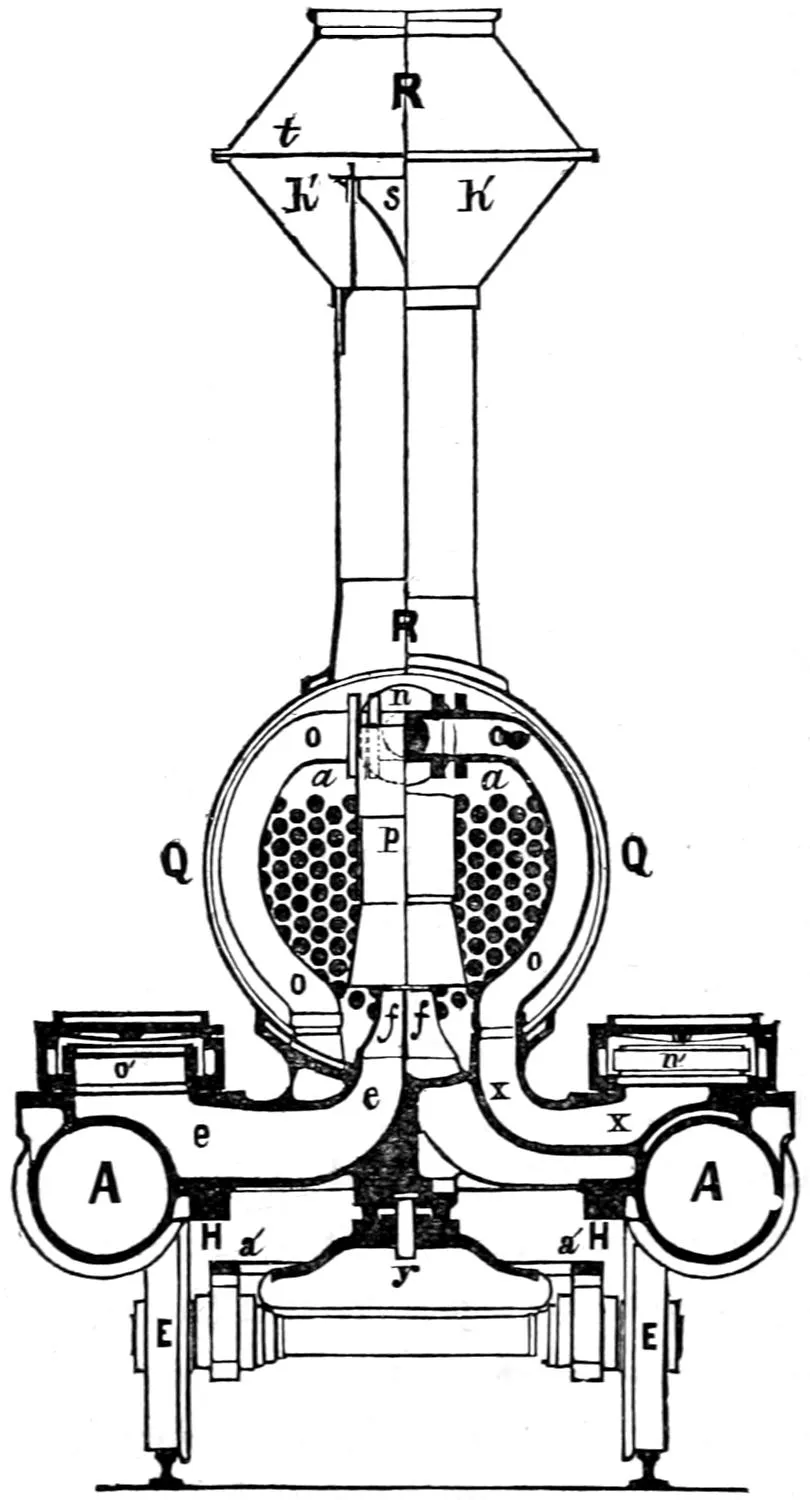
through crosswise, as shown in fig. 40, which is called
a transverse section. It is of course possible to represent
a transverse section of a machine like a locomotive
at a great many different points; for example, it
could be shown as though it was cut through the
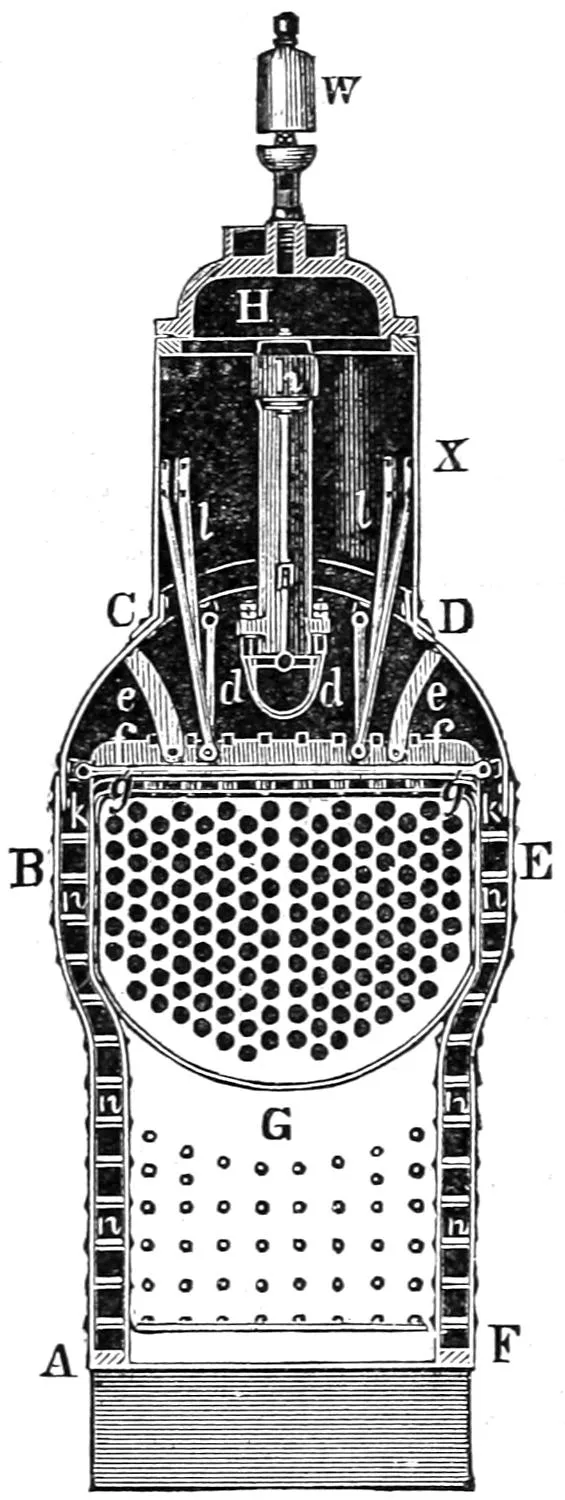
smoke-stack as in fig. 40, or through the boiler farther
back, as the latter is shown in fig. 42. Usually when
a section is shown through a cylindrical object like a
smoke-stack or boiler, it is shown through its centre.
If, however, this is not apparent from the drawing or
engraving, it should be stated at what point it is supposed
to be taken, thus the section D of the apple is
on the line a b of fig. A, and the section C is on the
line c d.
In drawing sections, the parts which are supposed
to be cut in two are usually shaded with parallel diagonal
lines drawn at equal distances apart, as shown in
the sections of the apple at C and D. Sections are
also sometimes represented with solid black surfaces,
as in Plates II and III, and in the engraving of a
pump in fig. 66.
Objects which are behind others which are in front
of them are often shown with dotted lines, so as to indicate
their position. The seeds of the apple are thus
indicated at A.
It is also customary, in drawings of machinery, to
take great liberties with the objects represented and
to show them with parts removed or broken away, if
their construction can thus be made plainer. It
should be remembered that the purpose of drawings of
this kind is not to give a pictorial representation of
the object as it appears to the eye, but to make its
construction and mode of operation apparent to the
mind. In such drawings therefore all perspective is
disregarded. It would lead us too far were we to explain
the reasons for this, and therefore readers must
accept the assertion without the proof.
PART I. THE STEAM ENGINE.
CATECHISM OF THE LOCOMOTIVE.
Question 1.What is the motive power employed in
ordinary steam engines?
Answer. The expansive force of steam.
Question 2.How is this expansive force of steam
applied?
Fig. 1.
Scale ³⁄₈ in. = 1 foot.
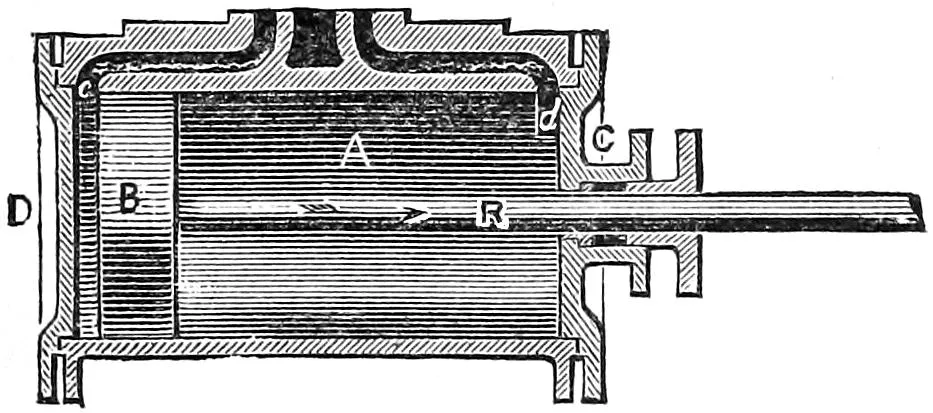
A. Cylinder. B. Piston. R. Piston-Rod. D. Front Cylinder-Head. C. Back Cylinder-Head.
Answer. It is applied by admitting it into a cylinder
(A, fig. 1) in which a piston, B, is fitted so as to move
air-tight from one end of the cylinder to the other.
The steam, if admitted at C, will force the piston B to
the opposite end[2] of the cylinder. When it has
reached that end, if the steam is allowed to escape
and a fresh supply is admitted to the cylinder through
the opening d, it will move the piston back again. In
this way, by alternately admitting steam at one end
and exhausting it from the other, the piston receives
a reciprocating motion, which is communicated to the
outside of the cylinder by a rod, R, which is called
the piston-rod, which works air-tight through an opening
in one of the cylinder-covers, or cylinder-heads, as
they are usually called.
[2] In all ordinary locomotives, the cylinders are so placed that the head
C through which the piston-rod works is behind, and the other head D
in front. The two ends of the cylinder are therefore designated the
front and back ends, respectively.
Fig. 2.
Scale ³⁄₈ in. = 1 foot.
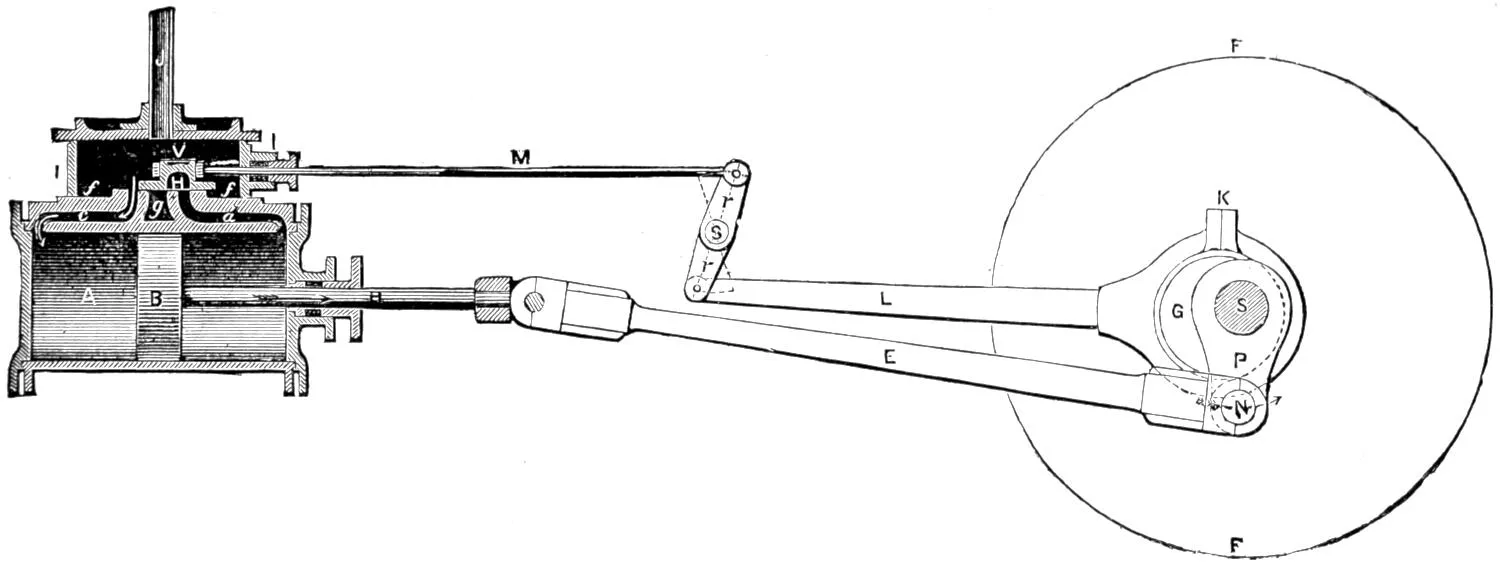
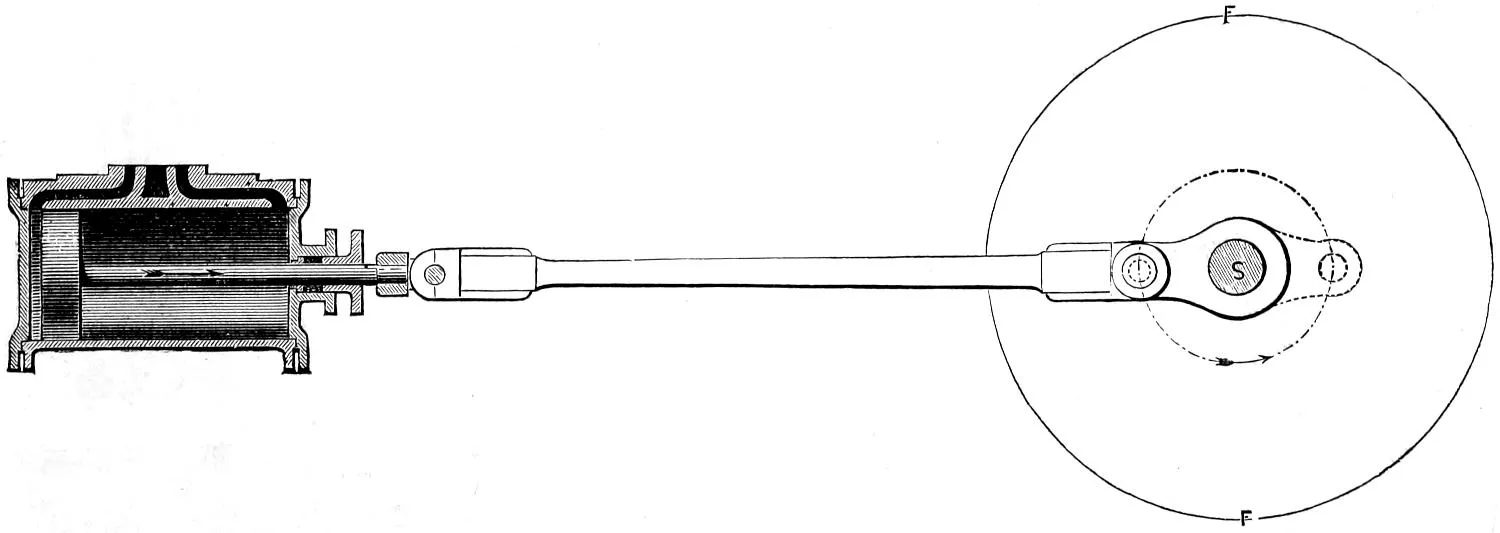
A. Cylinder. B. Piston. R. Piston-Rod. c. and d. Steam-ways. g. Exhaust-Port. V. Slide-Valve. H. Exhaust-Cavity. f.f. Valve-Seat. I. I. Steam-Chest. M. Valve-Stem. r.r. Rocker. F. F. Fly-Wheel. s. Rocker-Shaft. G. Eccentric. K. Eccentric-Strap. L. Eccentric-Rod. E. Connecting-Rod. P. Crank. N. Crank-Pin.
Fig. 3.
Fig. 4.
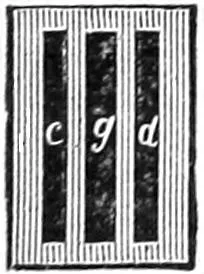
c. and d. Steam-Ports. g. Exhaust-Port.
Fig. 5.
Scale ³⁄₈ in. = 1 foot.
Question 3.How is this reciprocating motion of the
piston converted into rotary motion?
Answer. By connecting the end of the piston-rod R
(fig. 2) by another rod, E; called a connecting-rod, with
a crank, P, which is attached to a revolving shaft, S.
It is apparent that if the piston B is moved in the
direction shown by the dart R, a rotary motion will be
given to the crank in the direction of the dart N.
When, however, the crank reaches the position shown
by the dotted lines in fig. 5, it is plain that a force applied
to move the piston in either direction will no
longer produce a rotary movement of the crank and
shaft. The same thing will occur when the crank is in
the opposite position, shown by the full lines. These
two positions are called the dead-points of the crank.
Question 4.How is the crank of an ordinary steam
engine carried past the dead-points?
Answer. Stationary engines are usually provided
with a large and heavy wheel, called a fly-wheel (F F,
fig. 2) which is attached to the shaft S. This wheel
receives a sufficient amount of momentum from the
crank, while the latter is moving from one dead-point
to the other, to carry it past those points.
Question 5.How is the steam admitted to and exhausted
from the cylinder?
Answer. It is admitted through two channels, c, d,
fig. 2, called steam-ways, cast in the cylinder. These
ways terminate in a smooth flat surface, f f, called
the valve-seat. Their openings in the valve-seat are
called steam-ports. Between them is another port or
cavity, g, called the exhaust-port, which communicates
with the open air. The form of these ports is
long and narrow, as shown in fig. 4, which represents
a plan of them. Over these ports a valve, V,
called a slide-valve, usually made of cast iron, with
a cavity, H, on its under side, is fitted so that by
moving it backwards or forwards it will alternately
cover and uncover the two steam-ports. The valve
and valve-seat are inclosed in a sort of box, I I, fig.
2, made of cast iron, called a steam-chest, into which
steam is admitted from the boiler by a pipe, J. When
the valve is in the position represented in fig. 2, the
front steam-port is uncovered and the steam is admitted
to the front end of the cylinder, and thus forces
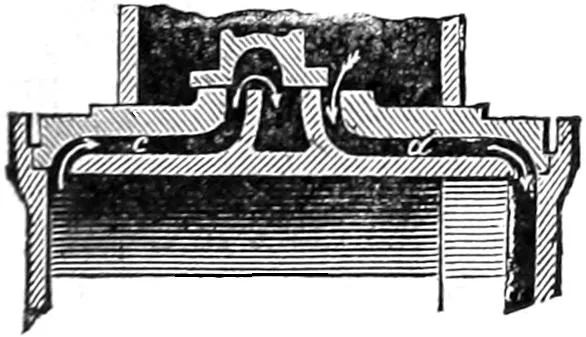
the piston towards the back end. If, when the piston
reaches the back end, the valve be moved into the
position shown in fig. 3, the back steam-port will be
uncovered and steam will be admitted to that end of
the cylinder. At the same time it will be observed
that the aperture of the front steam-port c and that
of the exhaust-port are both covered by the cavity in
the slide-valve, so that the steam which was admitted
to the front end of the cylinder can escape through
the steam-port c into the exhaust-port, and thus into
the open air. In this way, by moving the valve
alternately back and forth, steam is simultaneously
admitted first to one end and exhausted from the
other, and vice versa.
Fig. 6.
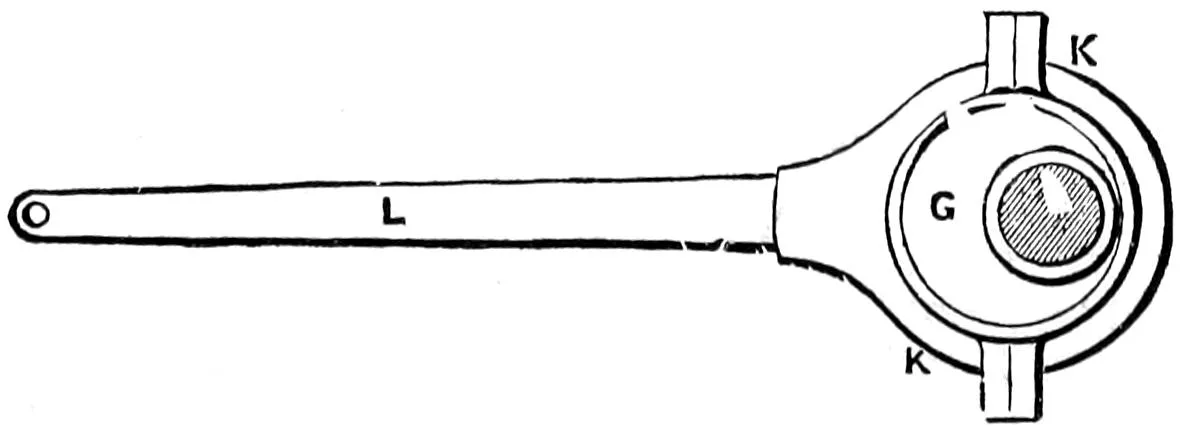
G. Eccentric. K. K. Eccentric-Strap. L. Eccentric-Rod.
Question 6.How is the slide-valve moved so as to
admit and exhaust the steam at the right time?
Answer. This is done by what is called an eccentric,
which is a circular disc, G (fig. 6), the axis of which
is not in the centre. The outside of the eccentric is
embraced by a metal ring, K K, made in two halves,
called an eccentric-strap. The eccentric is attached to
the shaft by screws or keys, and revolves with it and
inside of the eccentric-strap. To the latter is also
attached a rod, L, called an eccentric-rod. It is obvious
from fig. 6 that if the eccentric revolves inside of
the strap it will impart a reciprocating motion to the
rod L. The eccentric, G, strap, K, and rod, L, are
represented in fig. 2. Before describing their operation,
or rather their connection with the valve V, it
is necessary to understand that usually the valve-seat
is placed on top of the cylinder, in which position it
is difficult to connect the eccentric-rod with the valve.
For convenience, therefore, what is called a rocker, r r,
is placed between the cylinder and the main shaft of
the engine. This rocker has two arms attached to a
shaft, s, and the two arms have a vibratory motion
about it, as indicated by the dotted lines. The eccentric-rod
L is attached by a pin to the lower arm of the
rocker, and the valve is connected to the upper arm by
the rod M, called the valve-stem, or valve-rod. It is
obvious that as the shaft S and eccentric G revolve,
a reciprocating or vibratory motion will be given
to the rocker, which will be communicated to the valve
by the valve-stem; and it is only necessary to fix the
eccentric in the proper position on the shaft, in relation
to the crank and piston, to give the valve the required
motion for admitting and exhausting the steam
to and from the cylinder at the right time.
PART II. THE FORCES OF AIR AND STEAM.
Question 7.What is meant by the pressure of the
air?
Answer. It is the pressure exerted by the weight of
the air on every point with which it is in contact.
The globe of the earth is surrounded by a layer of air
about 50 miles thick, and, like every other substance,
the air possesses weight, and hence presses upon every
object with which it is in contact.
Question 8.How can it be shown that the air possesses
weight?
Answer. By weighing a flask when it is filled with
air, and again when the air is exhausted from it. In
the latter condition the weight of the flask will be
found to be sensibly less than it was when full of air,
showing that the air which the flask contained when
it was first weighed increased its weight.
Question 9.Why do we not feel this pressure on our
bodies?
Answer. Because the air surrounds us on all sides,
and presses just as much in one direction as it does in
another, so that the pressures in different directions
just balance each other, or are in equilibrium; but if
you disturb this balance, for example, by sucking the
air from a tube closed at one end, it will cling to your
tongue; or if you take a thick piece of leather under
ordinary conditions it will not adhere to anything,
but if it be thoroughly wet and pressed hard against
the surface of a smooth stone, so as to force out the
air from under it, the stone, as nearly all school-boys
know, can be lifted up if a string is attached to the
leather; or if the air be sucked out of a tube, one end
of which is inserted in a liquid, the latter will be
forced up the tube. These phenomena are due to the
pressure of the atmosphere in the first case on one
side of the person’s tongue, pressing it against the
mouth of the tube; in the second, to the same pressure
on the top of the leather, causing it to adhere to
the stone; and in the last, to the weight of the air
pressing on the surface of the liquid, forcing it into
the vacuum in the tube.
Fig. 7.
Scale ¹⁄₄.
Question 10.What is the amount of the pressure of
the atmosphere, and how is it measured?
Answer. It is usually measured by the pressure on
one square inch of surface, which at the earth’s surface
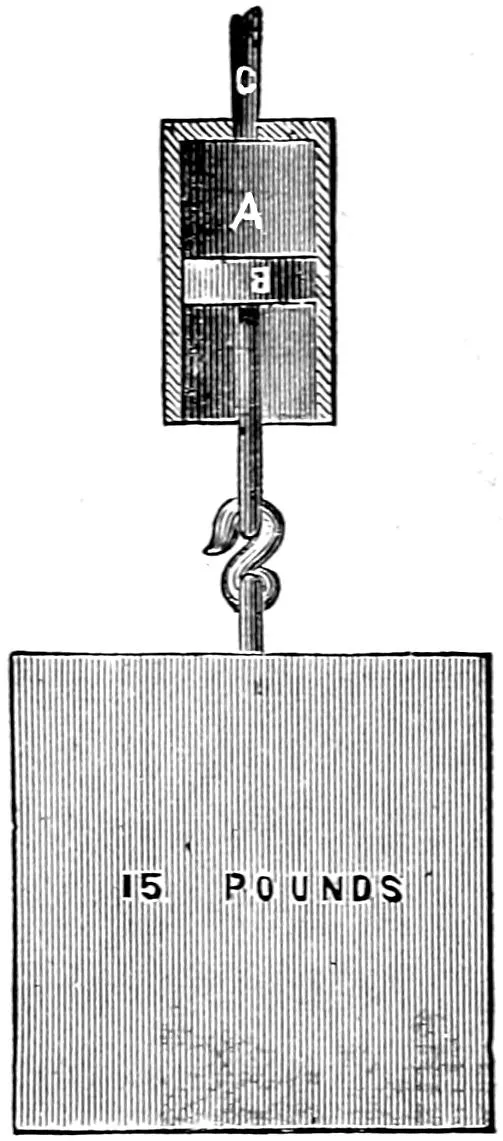
is 15 pounds.[3] If, for example, we have a cylinder,
A, fig. 7, with an air-tight piston, B, fitted to it
whose area is just one square inch, if we exhaust the
air through the tube C from the cylinder above the
piston, the air will press against the under side of the
piston so that, if no power is required to overcome its
friction in the cylinder, the pressure of the air will
raise a weight of 15 pounds. The pressure of the air
varies, however, as you ascend or descend from the
surface of the earth, because as you go up on a mountain
or in a balloon the layer of air above you becomes
thinner, and, therefore, its weight and consequent
pressure are diminished; and as you descend, as in a
deep mine, the layer is thicker, and its pressure consequently
greater.
[3] In common practice it is generally taken at 15 lbs. per square inch,
but the average atmospheric pressure is more accurately 14.7 pounds.
Question 11.What is steam?
Answer. Steam is water changed by means of heat
into a gas. At every temperature there is formed
from water, on its surface, vapor of which the clouds
are formed at all seasons of the year. This change of
water into vapor, or evaporation of water, takes place
at low temperatures only on its surface, however.
But if we heat water in a vessel to a temperature of
212 degrees Fahrenheit, then the inner particles of
the mass of water (lying on the heating surface of the
vessel) are changed into steam, and rise to the surface
in bubbles, which is the phenomenon we call boiling.
It must not be imagined, however, that the visible
cloud which escapes from a kettle or the exhaust-pipe
of a steam engine is true steam. It is rather small
particles of water, into which the steam has condensed
through contact with the cold air. True steam is invisible,
as we may observe near the mouth of a kettle
or the exhaust-pipe of an engine from which we know
it is escaping.
Question 12.If water is heated in an open vessel
what occurs?
Answer. It continues for some time to increase in
temperature, and the evaporation becomes more and
more rapid. At length bubbles of vapor break out
and reach the surface, and the process of boiling
or ebullition has begun. When this takes place
the temperature of the water ceases to rise, and it
remains stationary until all the water has boiled
away, the only difference being that if the supply of
heat be very great the process is very rapid, and if the
supply of heat be small the process is very slow. The
point at which ebullition commences is called the
boiling-point.
Question 13.On what does the boiling-point depend?
Answer. Chiefly on the pressure on the surface of
the water, but to some extent upon the purity of the
water. Thus, boiling, which takes place at 212 degrees
under the ordinary atmospheric pressure, in
lighter air, as on high mountains, takes place at a
much lower temperature than on lowlands, and so
water boils in a glass tube from which the air has
been exhausted by the warmth of the hand, that is, at
92 degrees.
Question 14.What is the pressure of steam which
escapes from boiling water in an open vessel?
Answer. It is exactly equal to the pressure of the
atmosphere in which it is boiled. Ordinarily this is
15 lbs., and the boiling-point 212 degrees; but if we
go up on a mountain where the atmospheric pressure
is only 10 lbs. per square inch, the water will then
boil at a temperature of 193.3 degrees, and the steam
which escapes will have the same pressure as the
atmosphere, or 10 lbs. per square inch. On the other
hand, if we could go down into a mine where the
atmospheric pressure was 20 lbs. per square inch, the
water would not boil until it was heated to 228 degrees,
and the pressure of the escaping steam would
then be 20 lbs. per square inch.
Question 15.If water is boiled in an enclosed vessel
like a covered tea-kettle or a steam boiler, what occurs?
Answer. The steam rises and fills the space above
the water, and, if it cannot escape, increases in pressure.
The temperature of both the water and the
steam rises with the pressure, and will continue to do
so as long as the heat is increased, or until the steam
can escape or the vessel is exploded. The boiling
point also rises as the steam pressure increases.
Question 16.Is there any pressure which corresponds
to the temperature of steam and water?
Answer. Yes. There is a fixed pressure for every
temperature, when steam is in contact with water,
and its pressure cannot be increased or diminished
without at the same time heating or cooling the water,
and the higher the temperature of the water the
greater will be the corresponding steam pressure.
Thus water at 212 degrees produces steam with a
pressure equal to that of the atmosphere; at 240 degrees
the steam will have a pressure of 25 lbs., or 10
lbs. more than the atmospheric pressure; at 281 degrees
a pressure of 50 lbs.; and at 328 degrees, 100
lbs. As this relation of pressure to temperature is
fixed, if we know the one we can tell the other. This
is true, however, only where the steam is in contact
with water, when it is called saturated steam. If it is
separated from water it may be heated to a higher
temperature, and is then called superheated steam.
Question 17.How is the pressure of steam measured?
Answer. In the same way as that of the atmosphere,—that
is, by the force exerted on one square
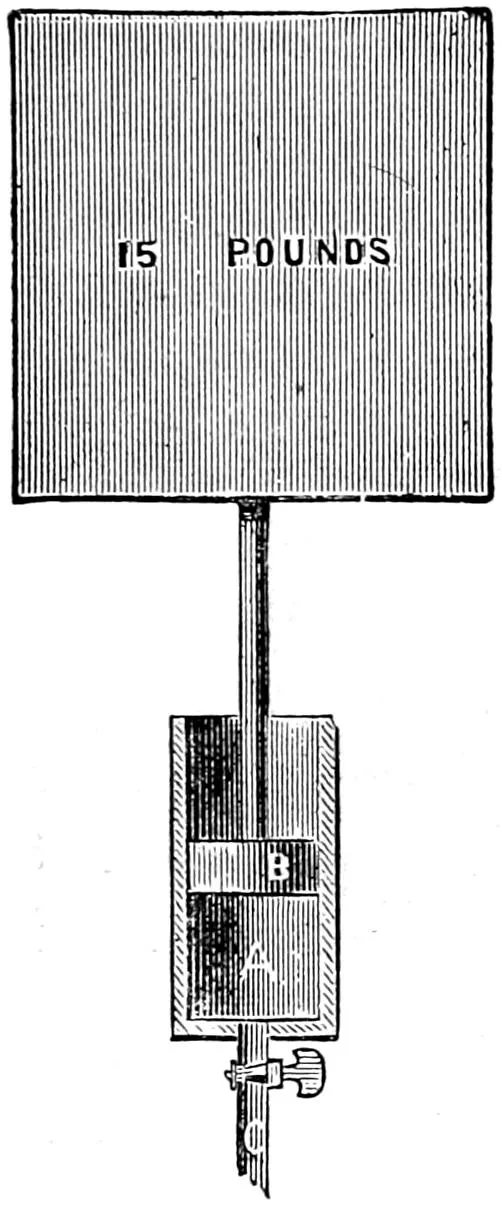
inch of surface. Thus if steam is admitted into the
cylinder A, fig. 8, under the piston B, whose area is
equal to one square inch of surface, supposing, as we
did before, that no power is required to overcome its
friction in the cylinder, if the steam thus admitted
would just balance the atmosphere, its pressure would
be equal to 15 lbs. If, besides overcoming the pressure
of the atmosphere, it would raise a weight of 15
lbs., then its pressure per square inch would be equal
to 30 lbs. When the atmospheric pressure is included
with that of the steam, we call it the absolute steam
pressure. In ordinary engines, however, the steam
must always overcome the pressure of the atmosphere,
and therefore the only part of the pressure which is
effective is that above, or by which it exceeds, the
atmospheric pressure. For example, although the
steam admitted under the piston in fig. 8 has an absolute
pressure of 30 lbs. per square inch, yet it will
only raise a weight of 15 lbs., because it must first
overcome the pressure of the air on the other side of
the piston. The pressure of the steam used in most
stationary and in locomotive engines is, therefore,
measured by its pressure above the atmosphere. That
is, if steam introduced under the piston in fig. 8 will
raise a weight of only 15 lbs., we say it has a pressure
of 15 lbs. per square inch; if it will raise 50 lbs., its
pressure is said to be 50 lbs. per square inch, and so
on. The pressure of the atmosphere is disregarded,
and all steam-gauges used on locomotives are graduated
in that way. In speaking of steam pressure in
future, therefore, unless otherwise specified, we shall
mean effective and not absolute pressure.
Fig. 8.
Scale ¹⁄₄.
Question 18.What is meant by the expansion of
steam?
Answer. In all gases a repulsion is exerted between
the various particles, so that any gas, however small
in quantity, will always fill the vessel in which it is
held. Steam possesses this same property, and if
placed in any vessel the particles in endeavoring to
separate from each other will exert a force on all its
sides. This force we call the steam pressure. To
illustrate this we will suppose that the cylinder A in
fig. 8 is half filled with steam of 30 lbs. pressure. If
now the supply of steam is shut off, the steam in the
cylinder will expand so as to push the piston upward,
but with a somewhat diminishing force, the nature of
which we will explain hereafter.
Question 19.What is meant by the volume of steam?
Answer. It means the space which the steam occupies.
Question 20.What is the proportion which exists
between the volume and the pressure of steam?
Answer. If the temperatures remain the same they
are INVERSELY PROPORTIONAL TO EACH OTHER;
that is, the one increases in the same proportion as
the other diminishes. If we admit steam of 30 lbs.
pressure per square inch into the cylinder A, fig. 8,
and then cut off the supply by closing the cock C
and allow the steam in the cylinder to expand to
double its volume by pushing the piston to the end of
the cylinder, the steam pressure will then be only 15
lbs.; if it should expand to three times its volume its
pressure would be only one-third, or 10 lbs. per square
inch. This method for calculating the pressure of
steam after it has expanded is correct only for the absolute
and not for the effective pressures of steam. In
order to ascertain the effective pressures of steam after
expansion, it is only necessary to make the calculation
with the absolute pressure and deduct the atmospheric
pressure from the result. If, after being
thus expanded, the piston be pushed down again
so as to compress the steam into its original space, its
pressure will again be 30 lbs., providing no heat has
been lost in any way.
Question 21.With a cylinder of any given stroke[4]how can we determine approximately the pressure of the
steam after expansion for any given point of cut-off?[5]
[4] The stroke of a piston is the distance it moves in the cylinder, and in
ordinary engines is always twice the length of the crank measured from
center to center of the shaft and crank-pin.
[5] The steam is said to be cut off when the steam-port by which steam
is admitted to the cylinder is closed by the valve.
Answer.By multiplying the absolute pressure
per square inch of the steam in the cylinder
before it is cut off, by the distance
from the beginning of the stroke at which
it is cut off, and dividing the product by
the whole length of the stroke. Thus, if we
have a cylinder whose piston has a stroke of 24
inches, if we cut off the steam at 8 inches, and have
an ABSOLUTE pressure of 90 lbs. in the cylinder, the
calculation is as follows:
90 × 824
= 30 lbs. final pressure.
If we cut off at 10, 12 and 15 inches, the final pressure
would be 37¹⁄₂, 50 and 56¹⁄₄ lbs., respectively. To
get the effective pressure deduct the atmospheric pressure
from this result.
Question 22.What is the proportion between the
volume of steam and that of the water from which it is
formed?
Answer. At the pressure of the atmosphere (15 lbs.)
each cubic inch of water will make 1,610 cubic inches
of steam. At double that pressure, or 30 lbs. absolute
pressure, it will make a little more than half as much,
or 838 cubic inches; at four times, or 60 lbs. absolute
pressure, 437 cubic inches, or a little more than a
fourth as much as at the pressure of the atmosphere.
Question 23.Why is it that the quantity of steam at
high pressures is somewhat greater than in inverse proportion
to the pressure?
Answer. Because the boiling-point of water, as has
already been explained, is higher as the pressure increases,
and therefore the temperature of the steam
produced at such pressure is also higher than at lower
pressures; and as all gases are expanded by heat,
therefore the volume of steam at the higher pressures
is somewhat greater than in inverse proportion to its
pressure, on account of being somewhat expanded by
its high temperature. To make this plain, if we take
a cubic inch of water and convert it into steam of
atmospheric pressure, its volume will be 1,610 times
that of the water, and its temperature 212 degrees.[6]
If we convert this quantity of water into steam with
a pressure double that of the atmosphere, the volume
of the steam will be 838 times that of the water and
its temperature will be 250.4 degrees. If the volume
of the steam were exactly inversely proportional to the
pressure, the cubic inch of water at double the atmospheric
pressure would make only 805 cubic inches of
steam; but as the boiling-point at that pressure is
38.4 degrees higher, the steam is expanded 33 cubic
inches by the increase of its heat due to the higher
boiling-point.
[6] More accurately, 213.1 degrees, if we call the atmospheric pressure
15 lbs., as we have.
A table in the appendix gives the pressure, temperature
and volume of saturated steam up to 300 lbs.
absolute pressure.
Question 24.What is meant by the condensation of
steam?
Answer. It is the reconversion of steam into water
by cooling it, or depriving it of part of its heat. It
has been shown that the temperature of water must
be raised to a certain point to generate steam of a
given pressure. If the process is reversed, and we
deprive the steam of a part of its heat, some of the
steam is then at once reconverted into water, or condensed,
and the pressure of that which remains will be
reduced just in proportion as the heat is lost. When
the temperature gets below 212 degrees under atmospheric
pressure, all the steam will be condensed. As
the useful work which steam can do in an engine is
due to its pressure, which in turn depends on its temperature,
any loss of heat will diminish its effective
power. For this reason, all waste of heat from a steam
engine should, as far as possible, be prevented.
Question 25.How is the heat of the steam wasted or
lost in an ordinary steam engine?
Answer. It is wasted in three ways: first, by conduction;
second, by convection; and third, by radiation.
Question 26.What is meant by these three terms?
Answer. 1. By conduction is meant that phenomenon
which is manifested when we put one end of a
metal bar two or three feet long into the fire and heat
it. The heat is then gradually conveyed from one
particle of the metal to that next to it until finally
the end of the bar farthest from the fire becomes so
hot that it cannot be touched. The heat is then said
to be conducted through the bar. In the same way
the metal of the boiler, pipes, cylinders and other
parts of the engine becomes heated on one side, and
the heat is thus conveyed to the outside of these parts.
2. The air with which they are surrounded then becomes
heated, and being then lighter than the cold
air, it rises and is again replaced with air which is
not heated. In this way the heat is conveyed away
by the air, and this phenomena is therefore called
convection.
3. If an iron plate be placed in front of an ordinary
grate fire three or four feet from it and exposed to the
rays of heat from the fire, it will soon become so hot
that you cannot bear your hand on it. If you place
your hand between the iron plate and the fire you
will find that only the side of your hand which is
exposed to the fire will become hot, showing that the
air between the plate and the fire is not nearly so hot
as the plate soon becomes, and therefore that the heat
is not conveyed to the plate by the air between it and
the fire, but by the rays from the fire. This phenomenon
is called radiation. The same thing occurs from
any hot body, as for example a coil of steam pipe for
heating a room, a steam boiler or cylinder of an engine.
Question 27.Is there any difference in the conducting
and radiating power of different substances?
Answer. Yes, very great. The difference in the
conducting power of wood and iron is shown if we
place one end of a bar of each in the fire. The wood
will be consumed without warming the bar more than
a few inches from the fire, whereas the iron will soon
become hot two or three feet from the fire. Owing to
the difference in the conducting power of cotton and
wool, we wear cotton clothing in summer and woolen
in winter, because cotton allows the heat of the body
to be conducted away from it, whereas woolen cloth
prevents to a great degree this loss of heat. For the
same reason, the venders of roasted chestnuts on our
streets wrap them in a piece of blanket to keep them
hot, that is, to keep the heat in; and in summer we
wrap ice in the same way to keep it cold, that is, keep
the warmth of the air out. The wool, being a very
bad conductor of heat, simply prevents the heat from
being transferred from the inside to the outside, and
vice versa. It is for this reason that steam boilers,
pipes and cylinders are nearly always covered with
wood, and sometimes with felt.
The difference in the radiating power of various
substances can be shown if we take a large thermometer
and heat it up to the temperature of boiling water.
If this thermometer is hung up in a room having the
temperature of melting ice, it will lose heat in two
ways,—first by heating the air which surrounds it,
that is by convection, and also by radiation. In order to
confine ourselves to the latter process, we will suppose
that the chamber is a vacuum. If we first cover the
bulb of the thermometer with a thin coating of polished
silver, and then ascertain how much heat it
radiates in a minute, and then coat it with lamp-black,
and repeat the same experiment,—that is to
say, allow the thermometer at the boiling-point to
cool for one minute in a vacuum chamber at the
freezing-point,—it will be found that the thermometer
loses much more in a minute when coated with
lamp-black than it did when coated with silver,
showing that much more heat is radiated from a
surface covered with lamp-black than from polished
silver. Generally it may be stated that polished
metals radiate much less heat than surfaces which
are not polished.[7] For this reason, as well as for
ornament, locomotive and other boilers and cylinders
are usually covered with Russia iron or polished brass.
[7] The account of the above experiment is copied from Balfour Stewart’s
very excellent little book, “Lessons in Elementary Physics,” of
which, and the same author’s “Elementary Treatise on Heat,” the
writer has made frequent use.
PART III. ON WORK, ENERGY, AND THE MECHANICAL EQUIVALENT OF HEAT.
Question 28.For what purpose are all steam engines
used?
Answer. They are used to produce motion, which is
opposed by some resistance. Thus, if an engine is
employed to raise grain from a railroad car to the top
of a warehouse, it must produce motion, which is resisted
by the weight of the grain; if it is used to
saw wood, it must give motion to the saw, which is
resisted by the fibres of the wood; a locomotive engine
must produce motion of a train of cars, which is
resisted by the air, the friction of the journals and the
rolling of the wheels on the track; if the locomotive is
employed on a grade or incline, besides the frictional
resistance referred to it must overcome that due to
its own weight and that of the train, which is gradually
lifted as it ascends the incline. In producing motion
opposed by some resistance an engine is said to be doing
“work.”
Question 29.Can this work be accurately measured?
Answer. Yes; but in order to measure anything we
must first establish some accurate standard or unit of
measurement. Thus we say a bar of iron is so many
inches long, or a road is so many miles long. In like
manner we speak of so many seconds, or minutes, or
hours, or days, or years, when we speak of time. So
it is necessary, in order to estimate or measure “work”
in a strictly scientific manner, for us to fix upon some
accurate standard or unit. In this country and in
Great Britain the unit agreed upon for this purpose is
the amount of power required to raise ONE POUND
ONE FOOT, and is called a foot-pound. If we raise one
pound two feet we do two foot-pounds of work; if
three feet, three foot-pounds, and so on. Again, if we
raise a weight of two pounds one foot high, we likewise
do two foot-pounds of work; or if we raise it two
feet high, we do four foot-pounds, and so on. In
order to determine the amount of work done, we must
MULTIPLY THE MOTION PRODUCED (in feet) BY THE
RESISTANCE (in pounds), AND THE RESULT WILL BE
THE WORK DONE IN FOOT-POUNDS.
Question 30.How many foot-pounds of work are
performed in a pile-driving machine in raising a weight
of 1,200 lbs. 24 feet?
Answer. 1,200 × 24 = 28,800 foot-pounds.
Question 31.When this weight is raised, is the force
which was exerted in raising it annihilated or lost?
Answer. No; because the weight has the capacity
of doing an equal amount of work when it falls, from
the momentum[8] it acquires in falling. This power of
doing work which it acquires in falling is called energy.
Now, although the weight has no motion-producing
power when it is raised to the top of the machine, yet
obviously such action is then possible which when it
rested on the earth was not possible. It has no energy
as it hangs there dead and motionless; but
energy is possible to it, and we might fairly use the
term possible energy to express this power of motion
which the weight possesses,[9] and which is therefore
called potential energy. As soon as the weight is allowed
to fall it acquires a greater velocity the farther
it falls, and its potential energy thus becomes and is
called actual energy.
[8] Momentum is not a very exact term, but is used here because it ordinarily
conveys the idea we wish to express.
[9] Tyndall’s “Heat Considered as a Mode of Motion.”
Question 32.How do we explain such phenomena
as the heating of a car-axle while turning under a car,
the heating of brake-blocks when the brakes are applied to
car-wheels, the heating of an iron rod by hammering, and
of a turning tool when cutting a piece of metal?
Answer. All of these phenomena are due to the fact
that the actual energy of motion is converted into heat,
as has been repeatedly proved by many able and ingenious
investigators and experiments.
Question 33.When the weight of the pile-driver
falls, is its energy also converted into heat?
Answer. A part is expended in compressing the
material into which the pile is driven and in overcoming
the friction of the earth against the pile, each of
which efforts develops heat, and another portion is
converted into heat by the impact or blow of the falling
weight on the head of the pile.
Question 34.Is all energy convertible into heat and
heat into energy?
Answer. Yes. Science has demonstrated very clearly
that they are mutually convertible.
Question 35.Has it been ascertained how much heat
is equivalent to one foot-pound of work?
Answer. Yes; it has been found, from the most
carefully-made experiments that the amount of heat
which is required to raise the temperature of one
pound of liquid water by one degree of Fahrenheit[10]
is equivalent to 772 foot-pounds of work. It must be
remembered that this is the theoretical equivalent of
heat, and that only a very small proportion of this
amount of work is ever realized from the heat developed
by the combustion of fuel.
[10] Thermometers are divided into different scales. The one called the
Fahrenheit scale, after its originator, is the one ordinarily used in this
country.
Question 36.If, then, heat is convertible into work
and work into heat, can the transmutation of the heat of
the steam in the cylinder of an engine into work, and the
reverse process, be explained?
Fig. 9.
Scale ³⁄₈ in. = 1 foot.
Answer. Yes. Take a cylinder, fig. 9, and, in order
to make the conditions of the experiment as
simple as possible, imagine it to be placed in
a vacuum. Now let saturated steam be admitted
under the piston so as to fill the cylinder
half full at an absolute pressure of 100 lbs. If we
will allow this steam to expand to double its volume
and raise the piston without doing any
work, and then repeat the experiment
with a load of 50 pounds on the piston,
whose area is one square inch,
it will be found that the temperature
of the steam is sensibly less, after
lifting the weight, than in the previous
experiment, in which it expanded
without doing work, showing that
part of the heat was abstracted from
the steam by doing work, or, in other
words, was converted into work. If
then, after the steam has expanded and lifted the
weight, we press the piston down so that the steam
under the piston is compressed to its original volume,
we shall find that its temperature is the same as before,
as the work done in compressing it is converted
into heat. In these experiments it is assumed that
there is no friction of the piston, nor loss of heat from
radiation or conduction. The same phenomena can
be observed in machines used for compressing air,
which is heated to so high a temperature when it is
compressed that it is necessary to cool the cylinders
of such machines by circulating a current of cold
water around them.
Question 37.What practical relation is there between
the convertibility of heat into work, and the conducting
and radiating properties of different substances
explained in answer to Question 27?
Answer. The fact that heat is only another form of
energy, or “the power of doing work,” indicates that
its loss by conduction or radiation lessens that power
just as much as or more than the loss or waste of coal
would, and therefore every effort should be made to
protect the different parts of engines from loss of heat
by covering them with substances which conduct or
radiate very little heat. Care should also be taken to
exclude cold air from circulating in contact with these
parts, and excepting for supporting combustion, the
nature of which will be explained hereafter, it should
be excluded from the heating surface of boilers.
Question 38.What is meant by the termLATENT
HEAT OF EVAPORATION?
Answer. By latent heat is meant that heat which
apparently disappears when water or other liquids are
vaporized. Thus, it is found that if any quantity of
water is converted into steam at any pressure, it is
necessary not only to heat it to a temperature equivalent
to that of the steam, or to the boiling-point, but
after it has reached that temperature an additional
amount of heat must be added in order to keep up the
process of boiling. Notwithstanding this addition of
heat to the water, the temperature of the steam produced
will not be higher than that of the boiling
water, thus showing that a considerable quantity of
heat is absorbed, the only effect of which is to change
the water into a gas or steam. This apparent disappearance
of heat can be shown if we take a pound of
boiling water whose temperature is 212 degrees and
mix it with a pound of ice-cold water at 32 degrees.
The result will be a mixture of two pounds of water
of a mean temperature of 122 degrees. If now we
convert a pound of water into steam at atmospheric
pressure, the steam will heat 6.37 lbs. of ice-cold
water up to 122 degrees, showing that a pound of
steam at atmospheric pressure contains over six times
as much heat as a pound of water of the same temperature
as indicated by a thermometer. A similar
apparent disappearance of heat occurs when other
liquids are evaporated, and when ice or any other
solid is converted into a liquid.
Question 39.What is the explanation of these phenomena?
Answer. The exact reasons which will explain them
fully are probably not yet clearly understood, but it is
at least extremely probable that when any substance
is changed from a solid to a liquid, or from a liquid to
a gaseous condition, “a large portion of the heat is
spent in doing work against the force of cohesion.”[11]
The particles of solid bodies, as we know, are so united
that it requires more or less force, according to the
nature of the substance, to tear them apart. Now we
can conceive that the heat is changed into a form of
energy, and in that condition resists this attraction of
the particles to each other, and that being thus transformed
it has lost the capacity of expanding the mercury
in the thermometer. A similar effect takes place
when a liquid is converted into a gas. In the former
condition the particles move freely about each other
and have little or no attraction for each other, but
when it becomes a gas they have a repulsion from
each other. The heat is thus converted into the
energy of repulsion, and therefore is in reality no
longer in the condition of heat and consequently does
not affect the thermometer. We can illustrate this by
supposing that by using steam heat is converted into
work by raising the weight, or drop as it is called, of
a pile-driving machine. When the weight is raised
to the top of the guides from which it falls, although,
as already explained, the heat is converted into potential
energy, yet if we attached a thermometer to the
drop we would not find that it was any warmer than
before the drop was raised. If it were possible to
make an instrument sufficiently sensitive to indicate
an instantaneous change of temperature in the weight
while falling, we would not find any increase of its
temperature at the instant it had acquired its greatest
momentum and just before it struck the object under
it, although its potential energy would at that instant
be converted into actual energy of motion. If, however,
the weight should strike an unyielding object,
its actual energy would at once be reconverted into
heat, which our thermometer would indicate. The
phenomenon of what is called latent heat of evaporation
seems to be very similar to that described—the
heat when the water is changed from a liquid to a
gaseous condition is transformed into energy, which,
as already stated, has no effect upon the mercury of
the thermometer.
[11] Balfour Stewart on the Conservation of Energy.
Question 40.What is meant by theTOTAL HEATof
steam?
Answer. The “total heat of steam” is a phrase used
to denote the sum of the heat required to raise the
temperature of water from some given point up to the
boiling-point due to a given pressure, and of the heat
which disappears in evaporating one pound of water
under a given pressure (or latent heat of evaporation.)
Thus the latent heat of one pound of steam at atmospheric
pressure (14.7 lbs.) is 966.1 units; and 212
units of heat are necessary to raise water from zero to
the boiling-point; therefore the total heat counted
from zero of steam of atmospheric pressure is 1,178.1
units. At 100 pounds absolute pressure the latent
heat is 885.5 and the sensible heat 327.9 degrees;
therefore the total heat measured from zero is 1,213.4
units.
PART IV. THE SLIDE-VALVE.
Question 41.What are the essential conditions
which a slide-valve must fulfill in governing the admission
and exhaust of steam to and from the cylinder of an ordinary
engine?
Answer. 1. It must admit steam to one end only of
the cylinders at one time. 2. It must allow the steam
to escape from one end at least as soon as it is admitted
to the other end; and 3. it must cover the steam-ports
so as not to permit the steam to escape from the
steam-chest into the exhaust-port.
Fig. 10.
Scale ³⁄₁₆ in. = 1 inch.
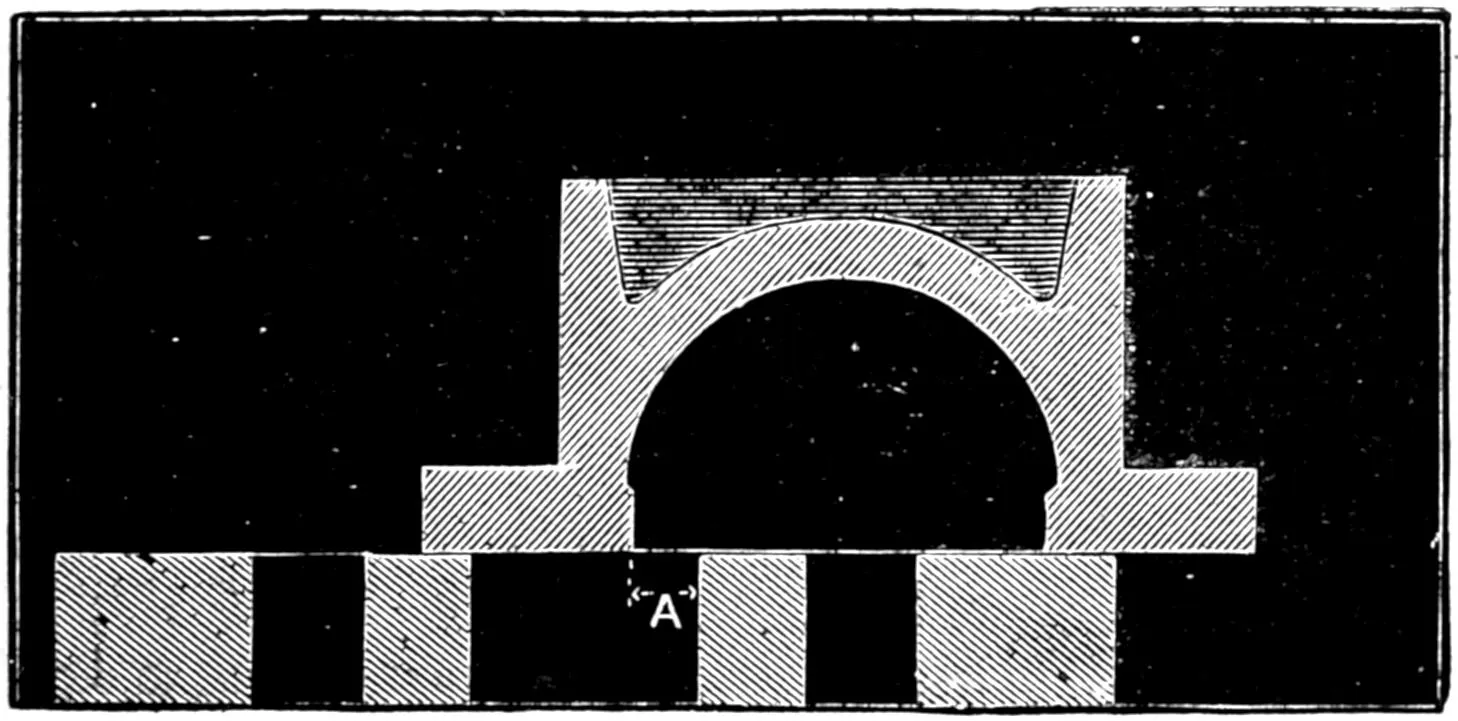
Question 42.What was the first form of slide-valve
used?
Answer. That represented in fig. 10. The smallest
movement of this valve either way opens one of the
steam-ports for the admission of steam and puts the
other in communication with the exhaust-port. By
cutting a piece of ordinary writing paper to the
form of the section of the valve, and moving it on
the line f f, the action of the valve will be clearly
shown.
Plate I.
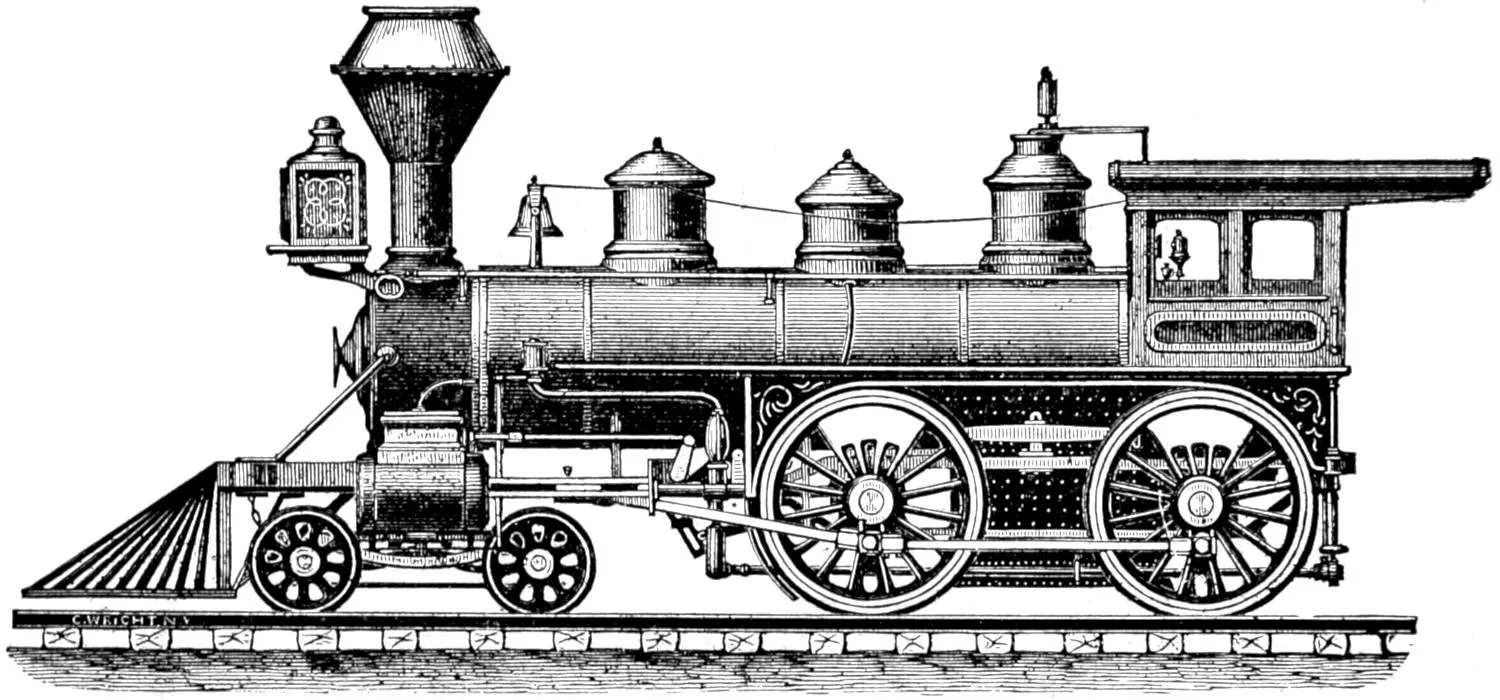
AMERICAN LOCOMOTIVE. By The Grant Locomotive Works, Paterson, New Jersey. Scale, ³⁄₈ in. = 1 foot.
Question 43.How was the admission and escape of
the steam effected by this valve?
Answer. In order to explain this clearly, a series of
diagrams will be necessary. Before referring to
them, however, it should be explained first that the
motion of an eccentric is exactly the same as that of
a small crank. It is in fact a crank with a crank-pin
whose diameter is very much enlarged. In the diagrams,
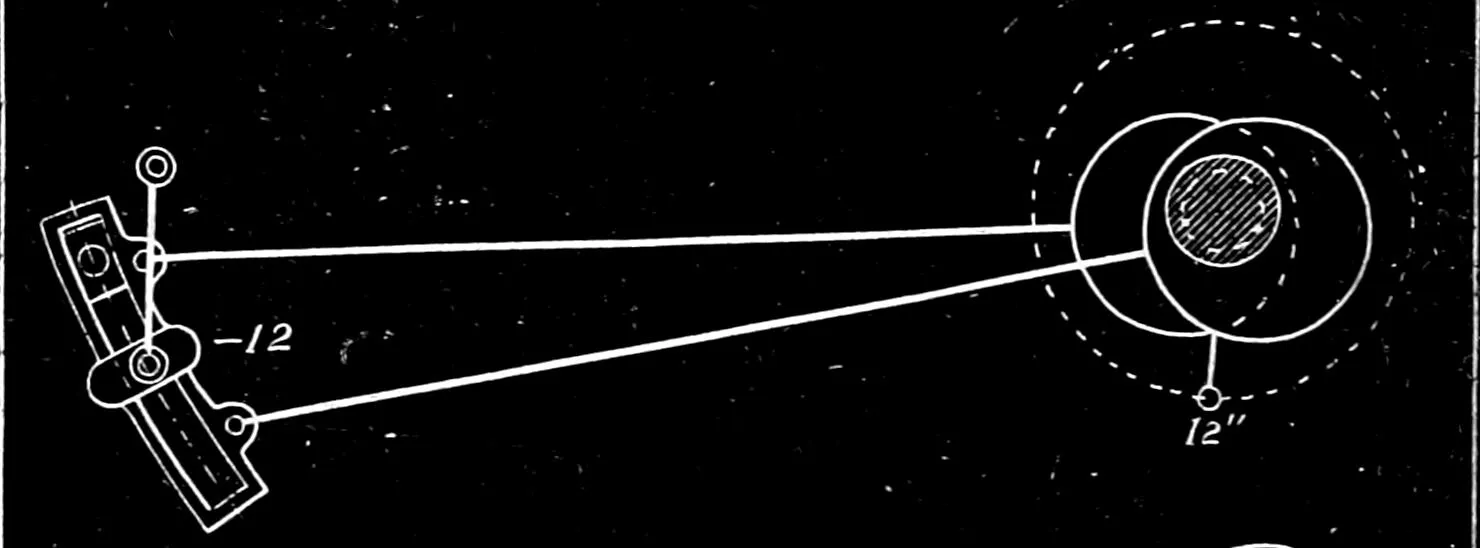
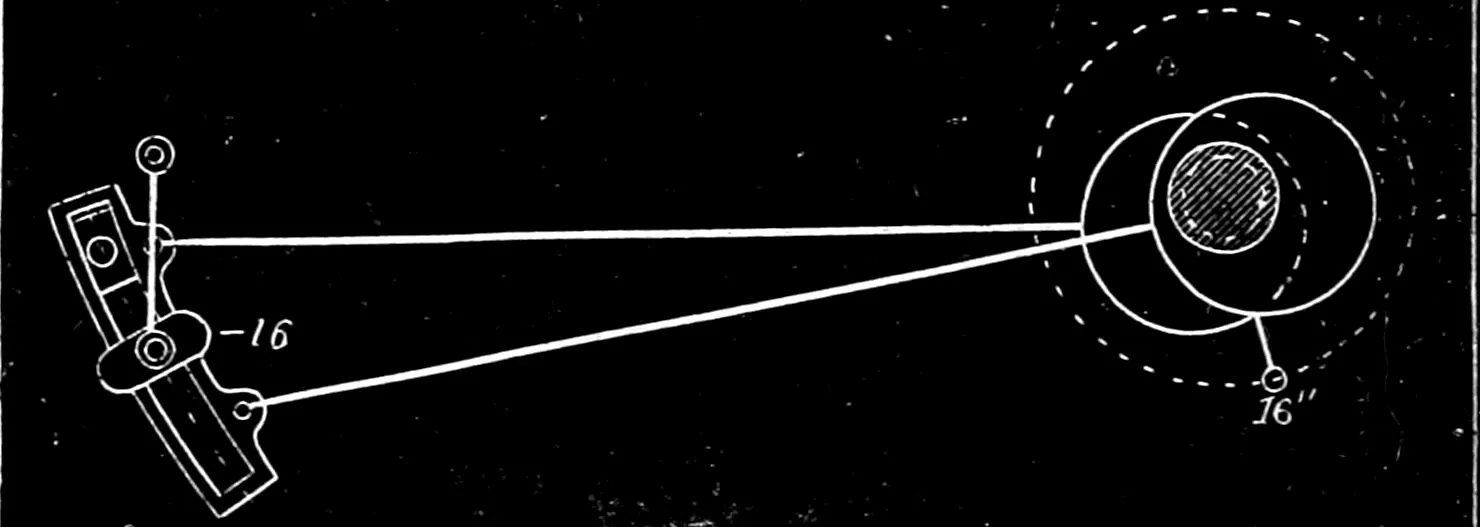
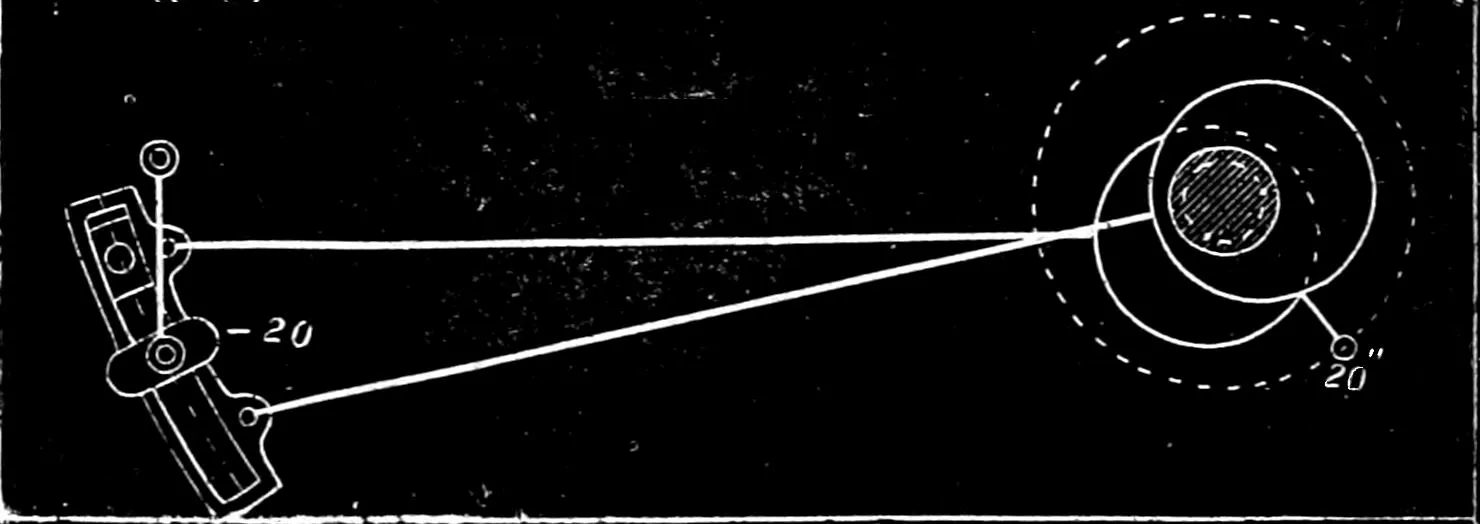
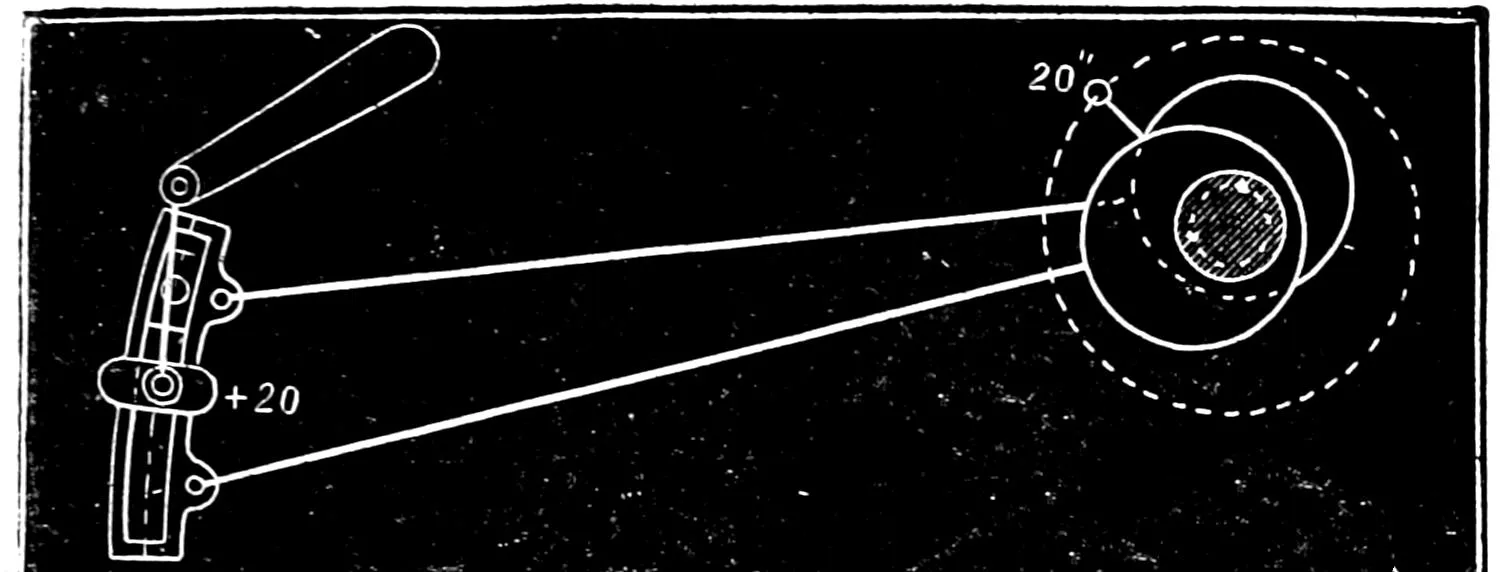
figs. 11 to 25, the eccentrics will therefore be
represented as small cranks, and most of the other
parts by their centre-lines and points only, so as to
make the diagrams as simple as possible. The dimensions
selected for these illustrations are for the cylinder
16 in. diameter and 24 in. stroke, and a connecting-rod
7 ft. long. The steam-ports are 1¹⁄₄ in., the
exhaust-port 2¹⁄₂ in., and the metal or bars between
them, which are called bridges, are 1¹⁄₈ in. wide. The
eccentric produces a lateral movement of 3 in., which
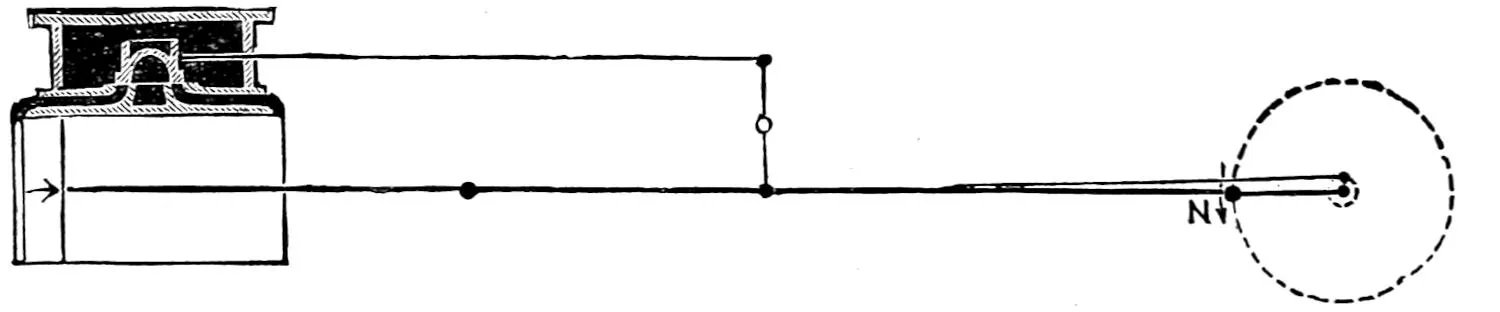
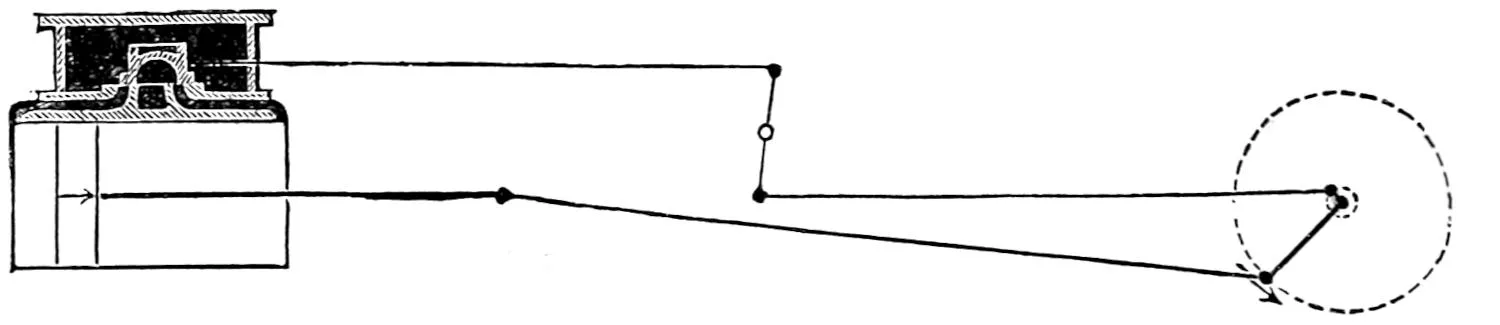
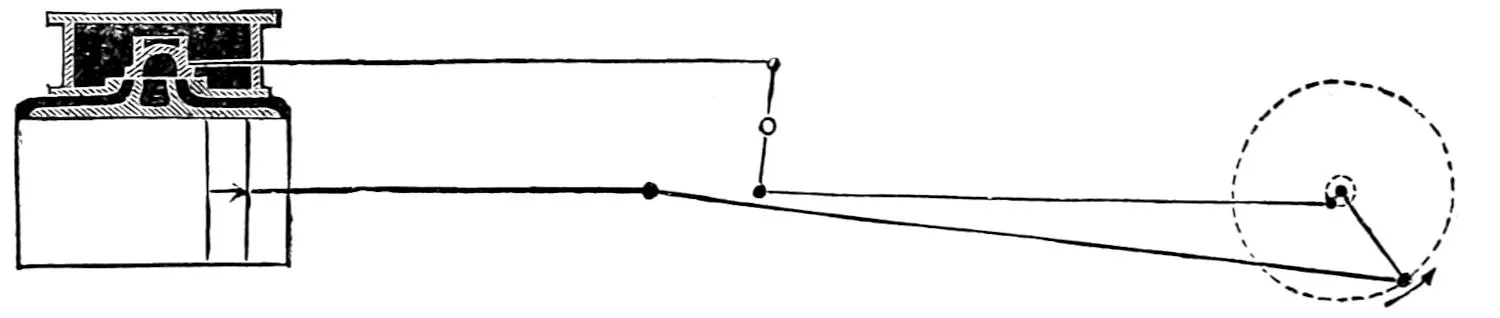
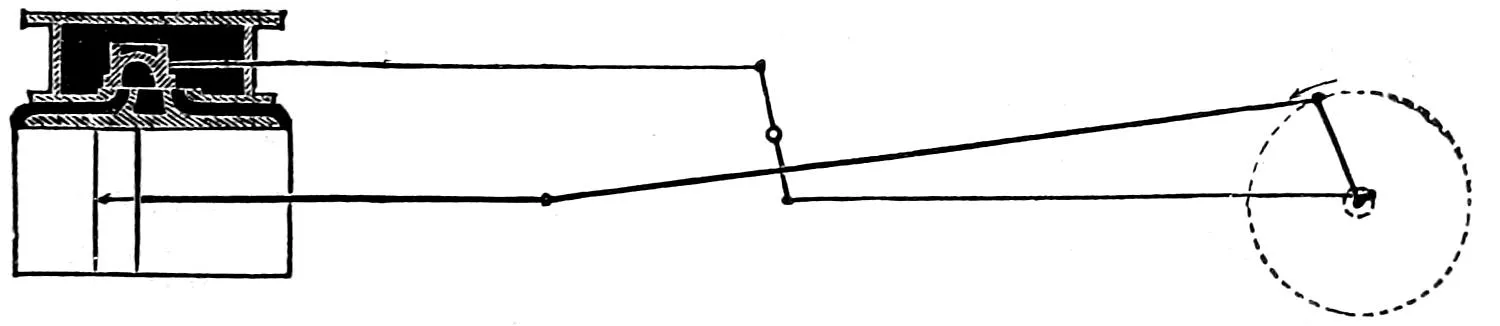
is called its throw. In fig. 11 the piston is at the beginning
of the backward stroke. The valve is then in
the centre of the valve-face, and the eccentric is consequently
at half-throw. The slightest movement of
the crank in the direction of the dart N will move the
eccentric enough to open the front steam-port to the
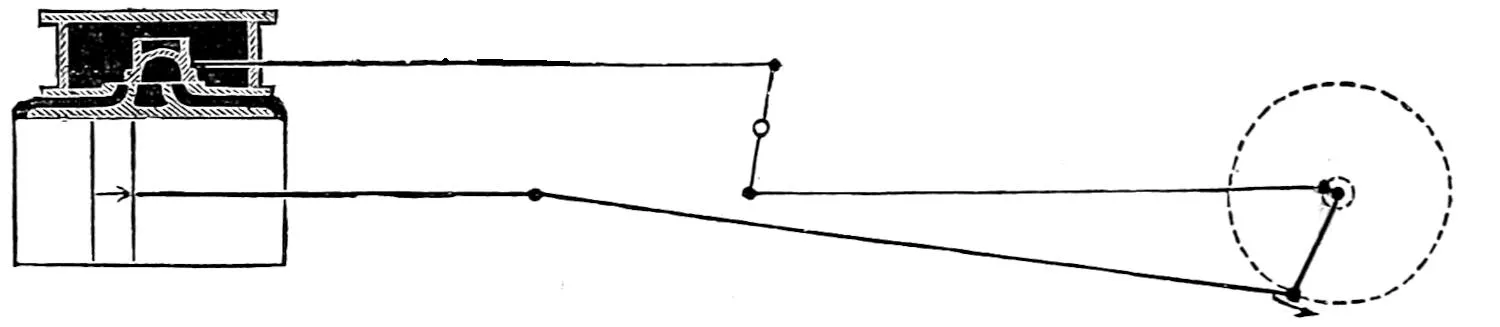
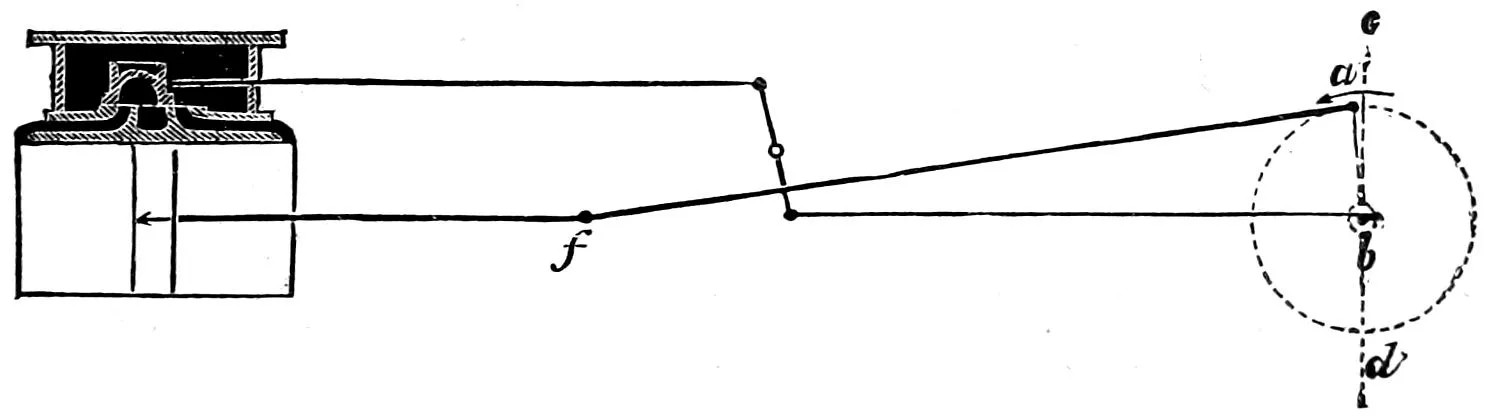
steam and the back one to the exhaust. In fig. 12
the piston is represented as having moved 4 in. of its
stroke; the valve has then partly opened the front
steam-port, and the other one is open to the exhaust.
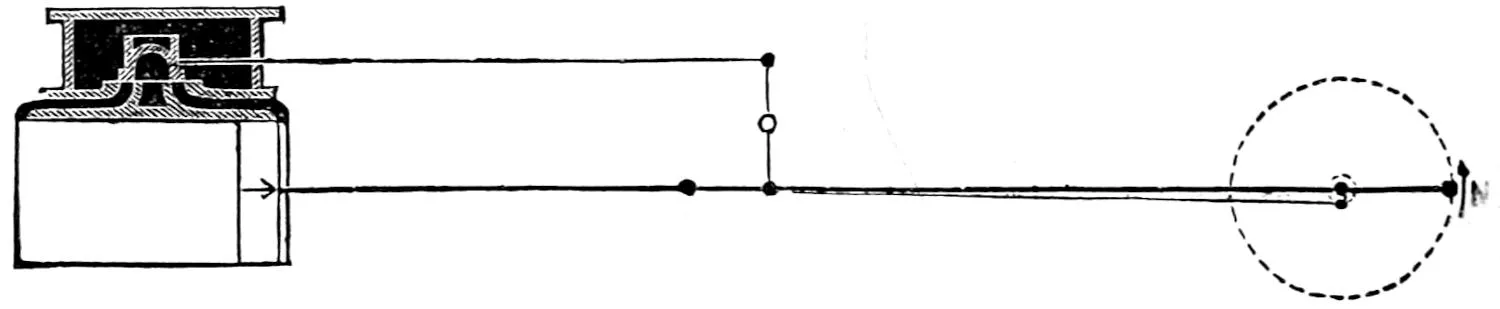
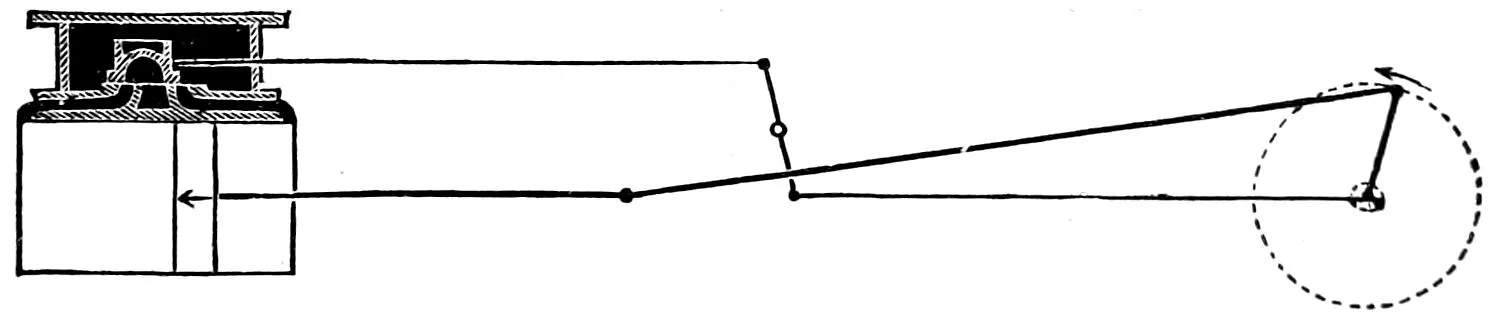
In fig. 13 the piston has moved 8 in. of its stroke, and
the ports are now wide open, the front one to the
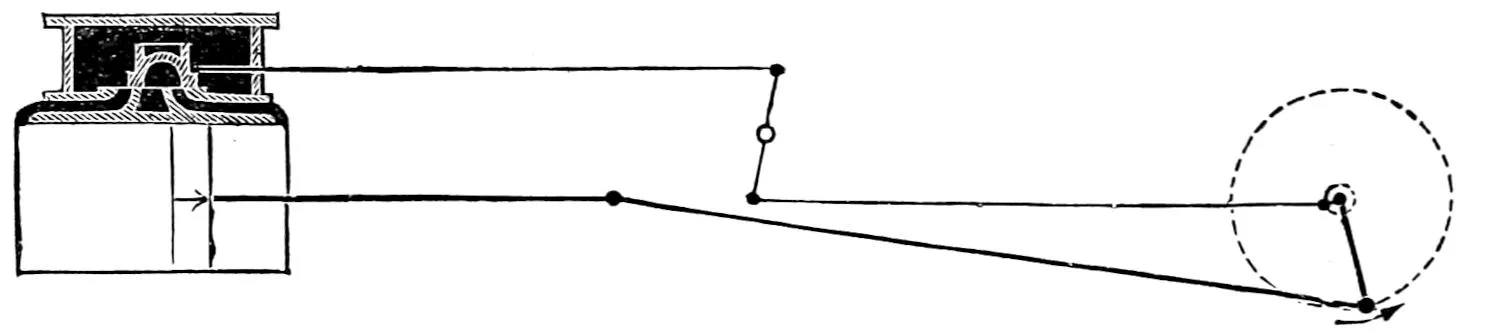
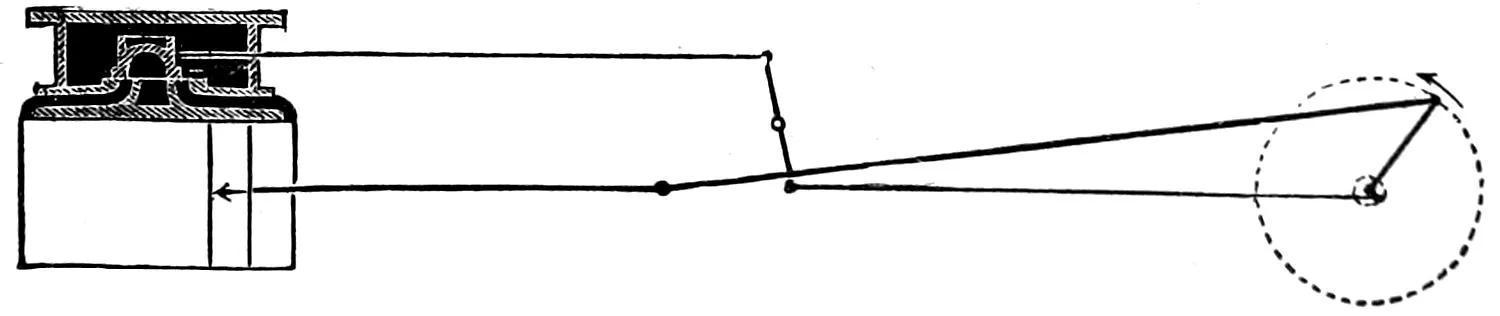
steam and the back one to the exhaust. In fig. 14
the piston has moved 12 in., or is at half-stroke, and
the valve has then moved as far as it will in that direction.
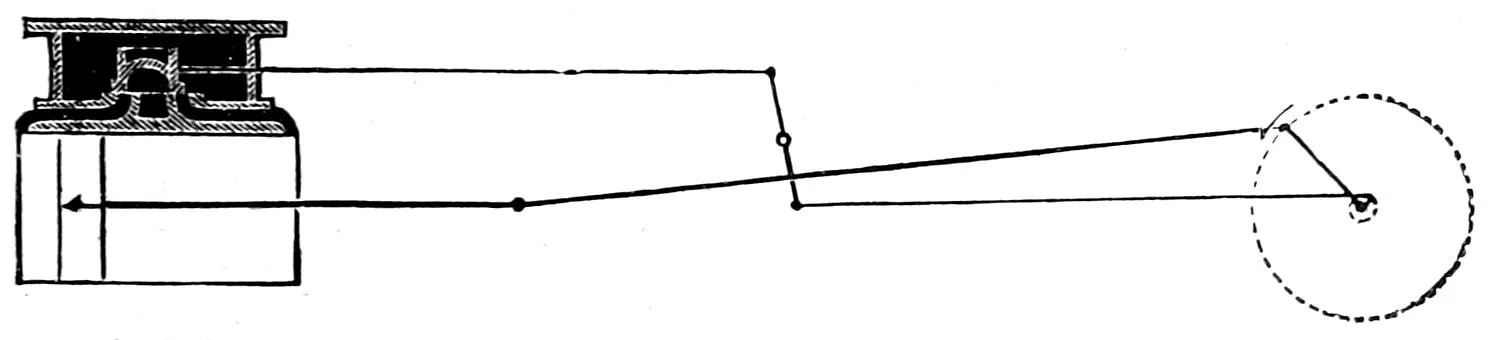
In fig. 15 the piston has moved 16 in. and
the valve has begun to return. In fig. 16 the piston
has moved 20 in., and the valve has nearly closed the
front port to the steam and the other to the exhaust.
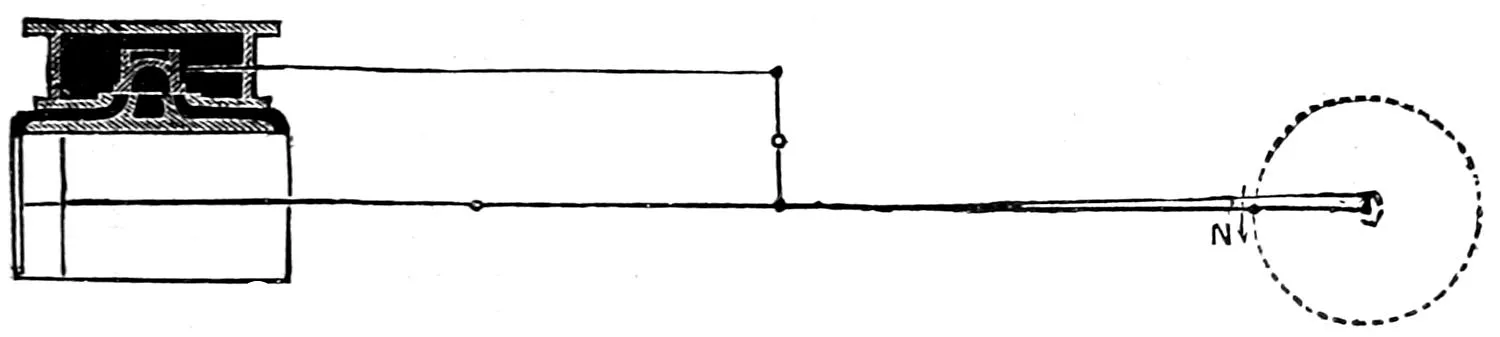
In fig. 17 the forward stroke is completed, and both
ports are closed by the valve. Figs. 18, 19, 20, 21,
22 and 23 represent the piston and the valve on the
return stroke in the positions corresponding with
those described for the backward stroke.
Fig. 11.
Fig. 12.
Fig. 13.
Fig. 14.
Fig. 15.
Fig. 16.
Fig. 17.
Scale ¹⁄₄ in. = 1 foot.
Fig. 24.
Fig. 23.
Fig. 22.
Fig. 21.
Fig. 20.
Fig. 19.
Fig. 18.
Scale ¹⁄₄ in. = 1 foot.
Question 44.Is there any other method by which the
motion of a valve can be represented by a drawing?
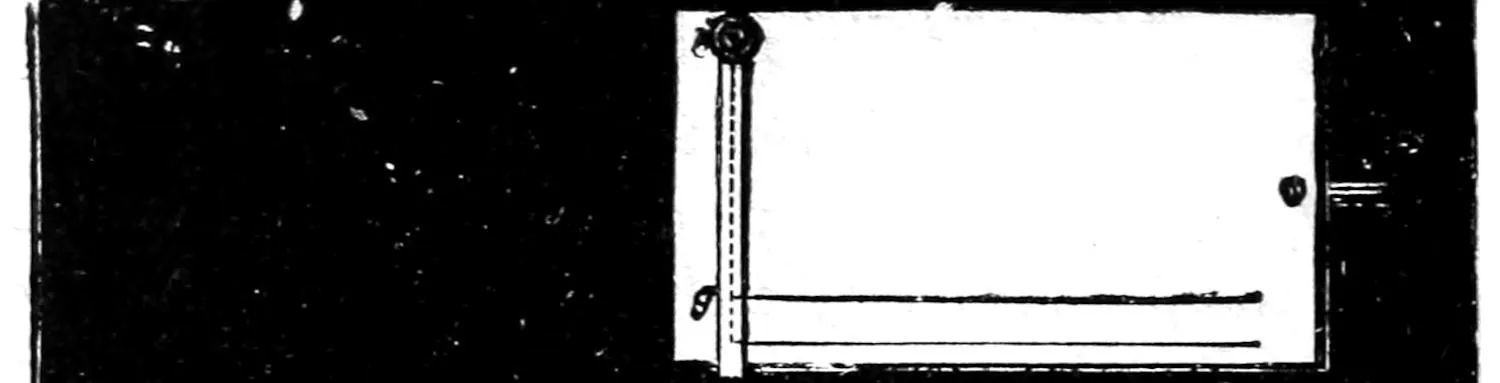
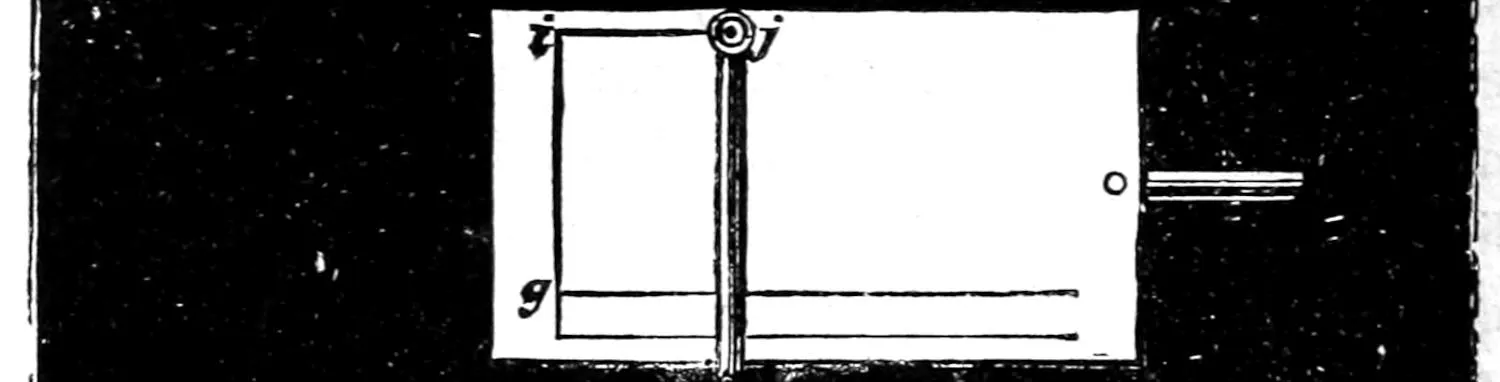
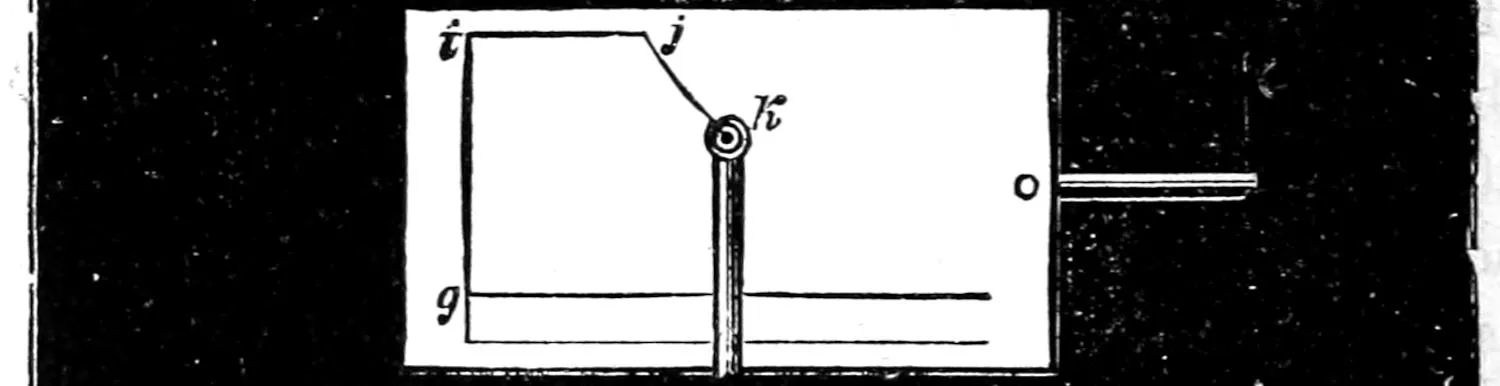
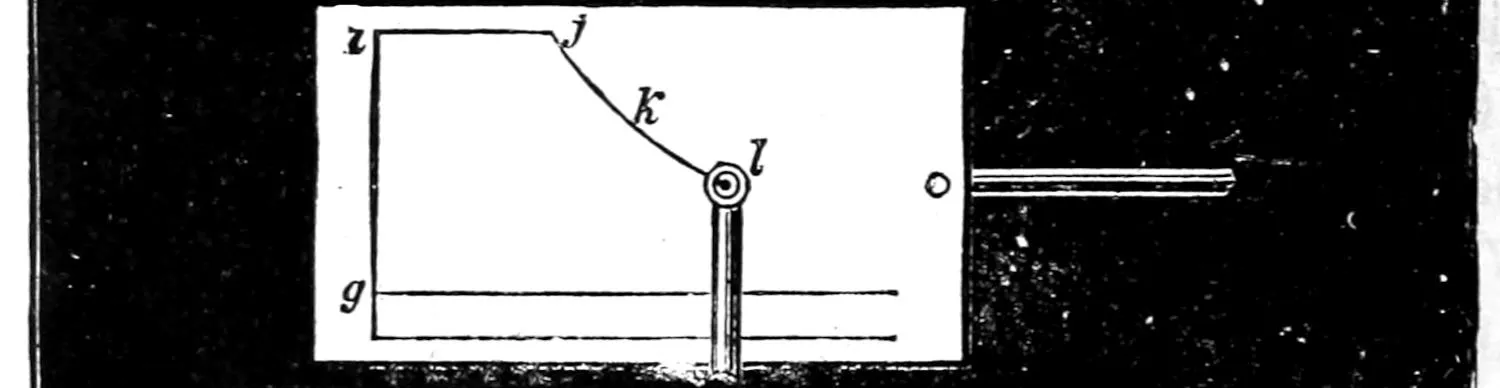
Answer. Yes, by what are called motion-curves. It
is, however, difficult to explain these clearly, and as
they are purely imaginary, it is difficult to understand
their nature and purpose. Close attention will therefore
be required to the following description:
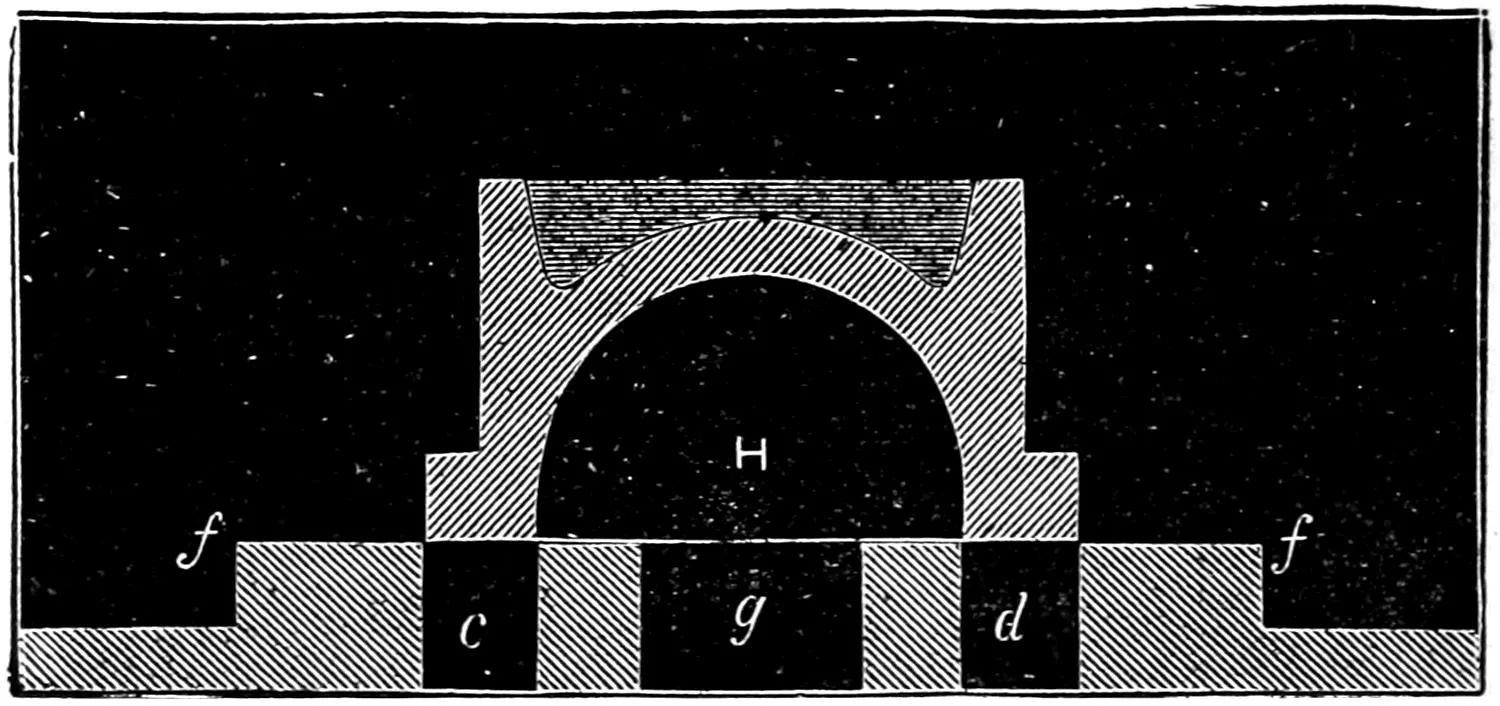
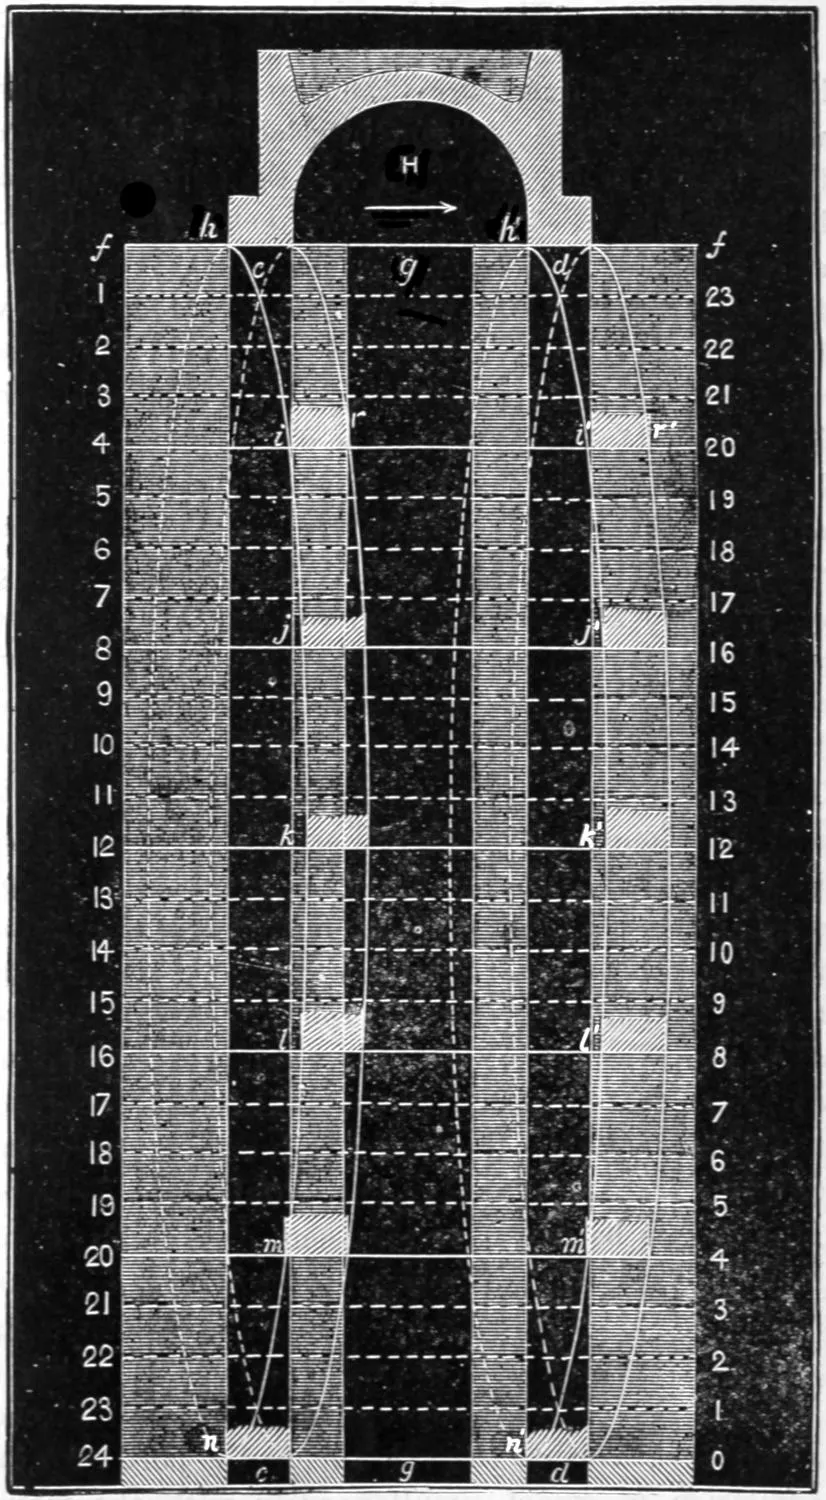
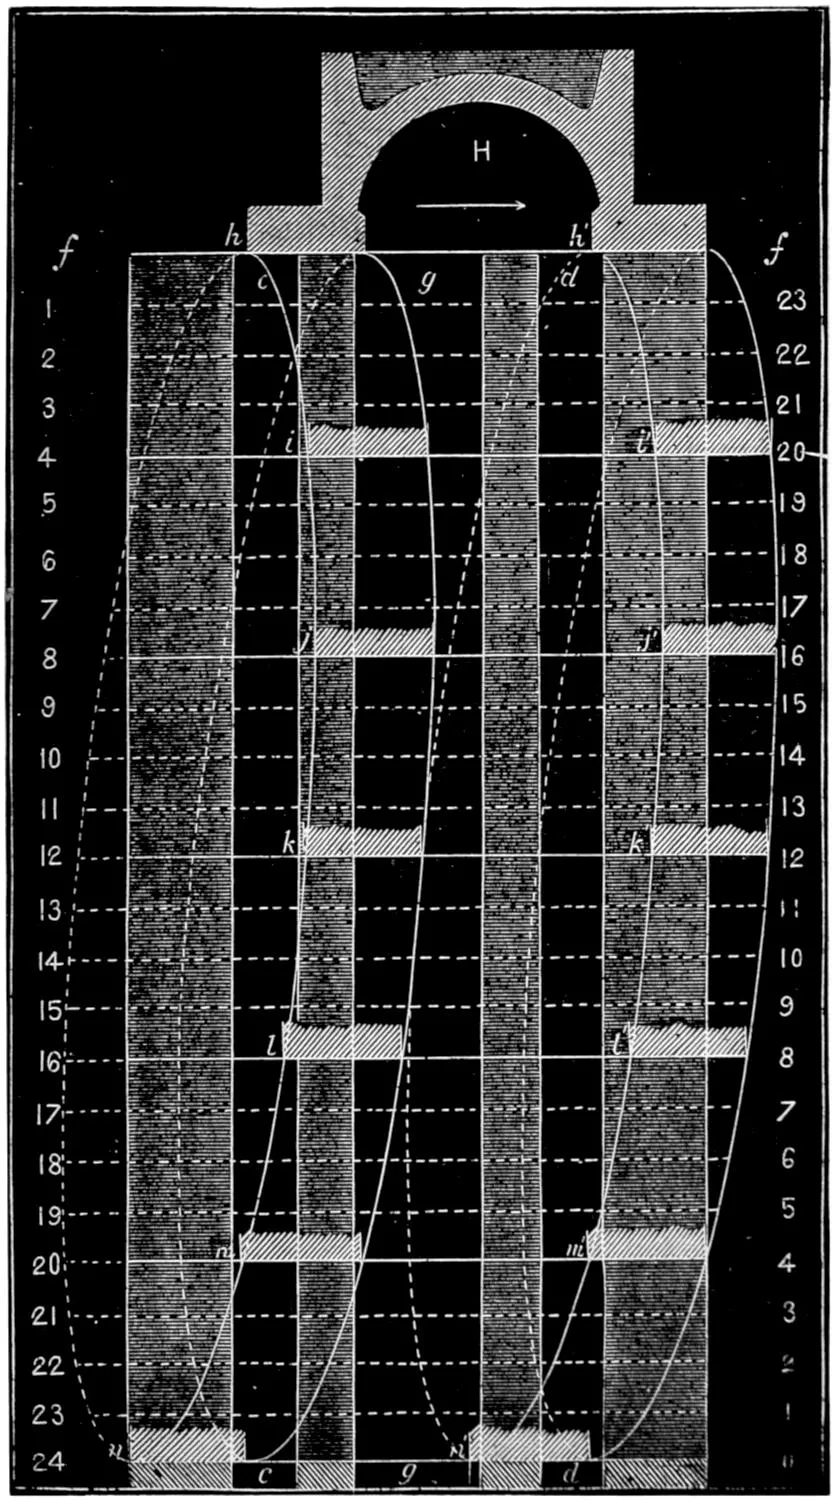
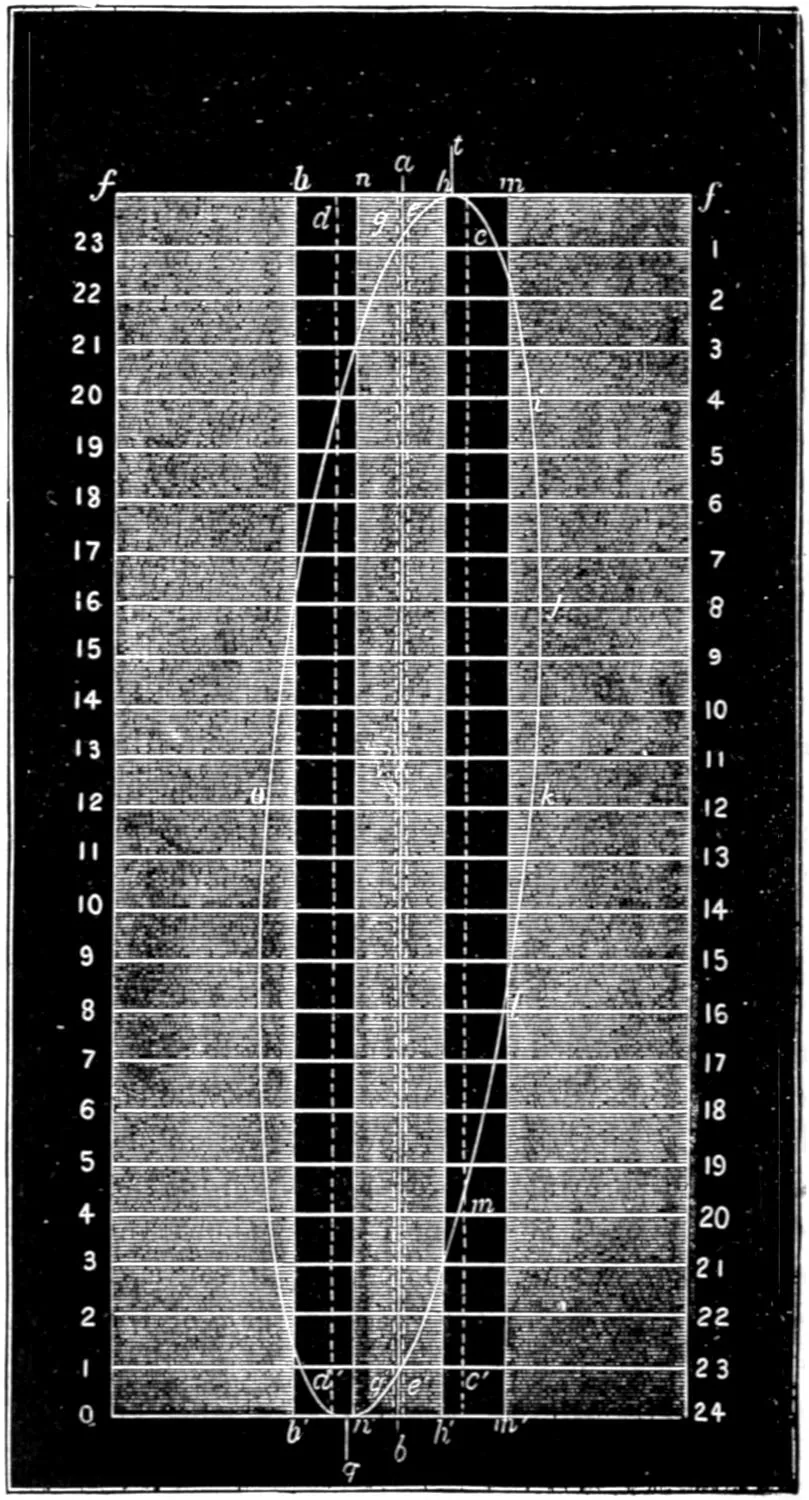
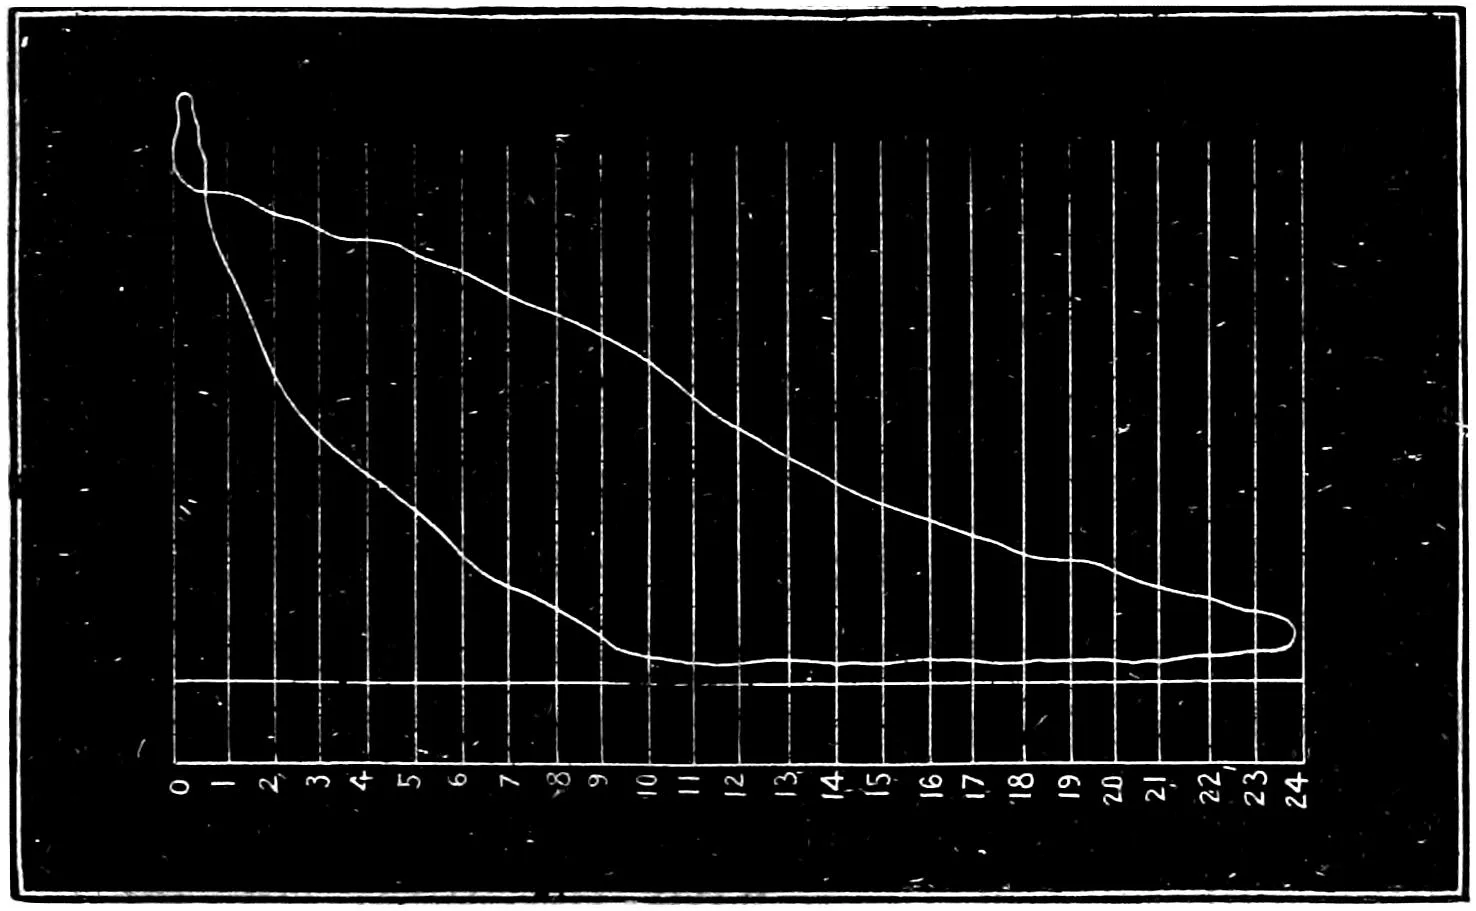
We will suppose, in the first place, that the line f f,
fig. 25, represents the valve-face, c and d the steam
and g the exhaust-port, drawn to a larger scale than
in the preceding figures. We will now draw the valve
H in the position represented in fig. 11, where the
piston is at the beginning of the stroke. In order to
show the valve in the position represented in fig. 12,
where the piston has moved 4 in. of the stroke, we
will draw a line 4-20, four inches below and parallel
to f f, and extend the lines, representing the edges
of the ports c, d and g, downward. On the horizontal
line 4-20 we will now draw the edges i, r, i′, r, of the
valve in the same position in relation to the port c
that it has in fig. 12. We will then draw another
horizontal line, 8-16, eight inches below f f, and parallel
to it, and on this represent the valve in the position
shown in fig. 13. In the same way we will draw
lines 12, 16, 20 and 24 in. below f f, and draw the
valve on each one respectively in the positions shown
in figs. 14, 15, 16 and 17. The distance between the
lower line 24-0, and f f, will then represent the
stroke of the piston, or 24 in. If now we begin from
the edge h of the valve on the line f f, and draw a
curve, h i j k l m n, through the same edge of the
valve, represented on each of the parallel lines below,
the curve will indicate the position of the valve in relation
to the steam-port c at each point of the stroke.
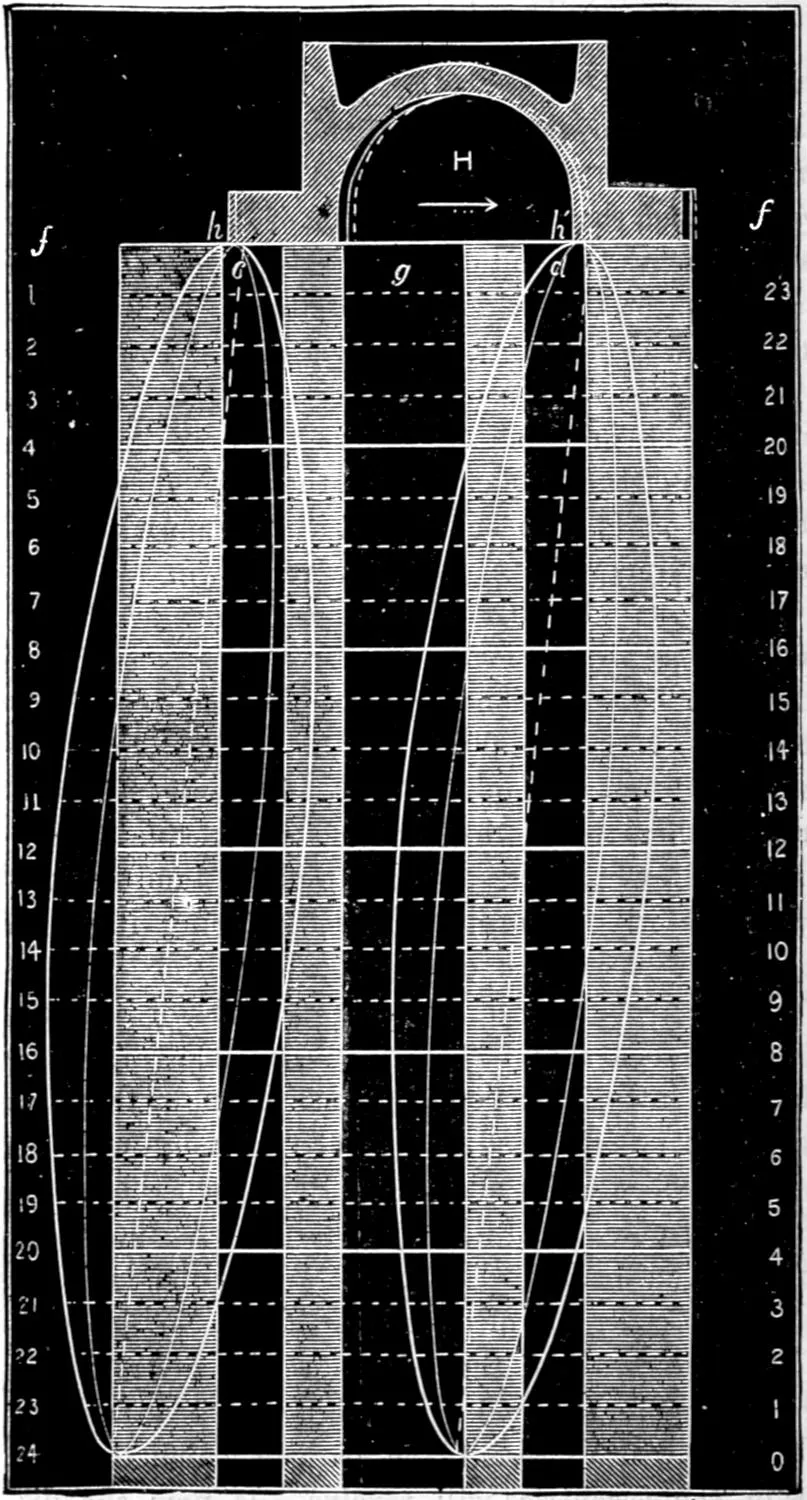
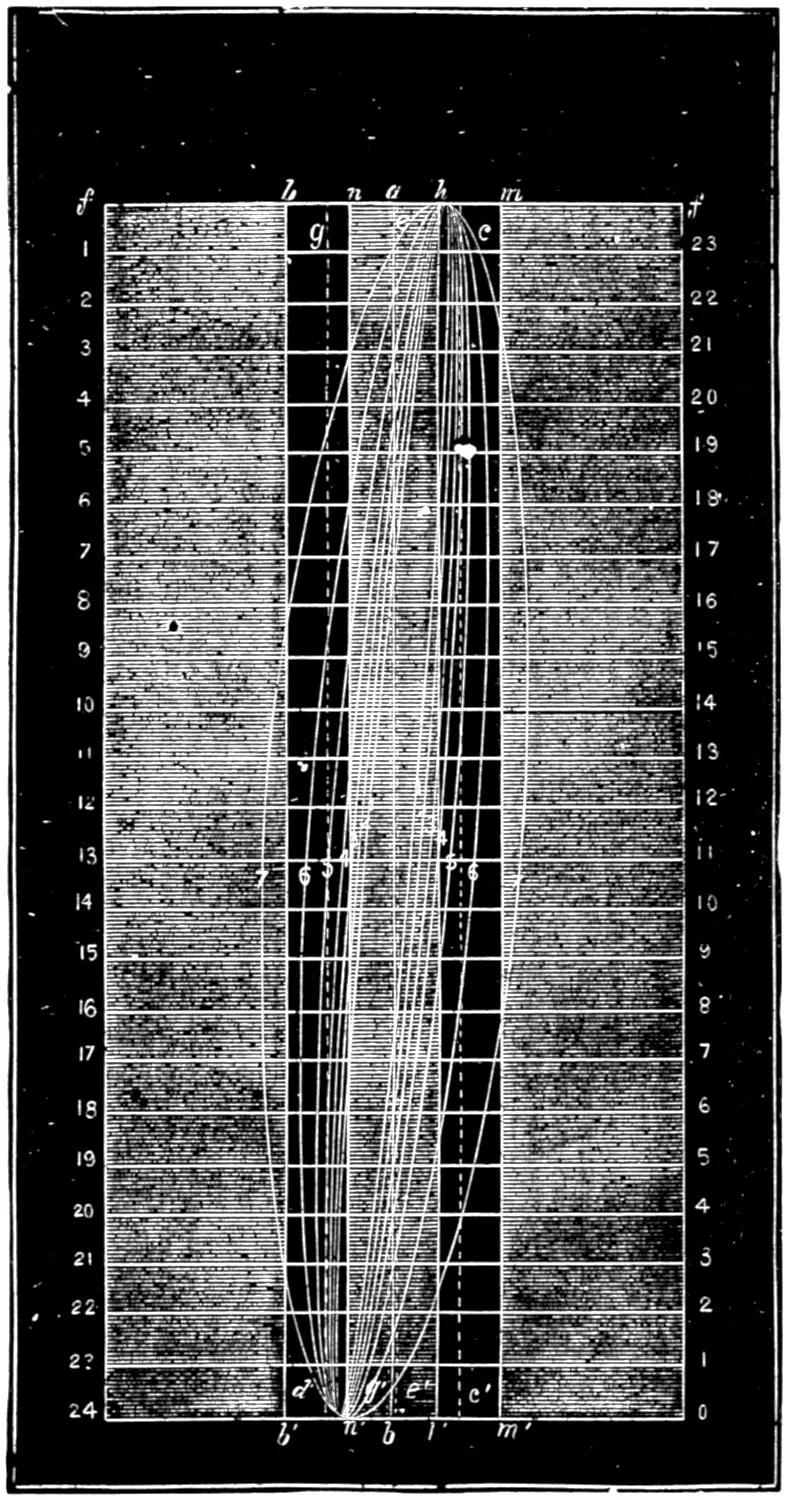
To illustrate this, suppose we draw lines 1-23, 2-22,
and 3-21, one inch apart and parallel to f f, and between
it and 4-20. They will then represent the position
of the piston after it has moved 1, 2 and 3 in.
from the beginning of the stroke, and where they intersect
the curved line will be the position of the edge
of the valve when the piston has moved 1, 2 and 3 in.
of the stroke. The curved line will in fact represent
the position of the valve at any point of the stroke between
these lines. Other horizontal lines, 5-19, 6-18,
etc., can be drawn to represent every inch of the
rest of the stroke. The curve line h i j k l m n, or
motion-curve as it is called, will then show the exact
position of the edge of the valve and of the width of
the opening of the steam-port during the whole stroke.
From it we see that the valve opens the port c for the
admission of steam simultaneously with the movement
of the piston, and when the latter has made one
inch of its stroke the port c is half open. At 4¹⁄₂
inches of the stroke the port is wide open,[12] and at 19¹⁄₂
inches it begins to be closed, but is not completely
closed until the end of the stroke.
[12] By cutting a paper section of the valve and placing it on the diagram
in each position named, it will probably help the reader to understand
the movement of the valve more and the nature of the motion-curves.
Fig. 25.
Scale ³⁄₁₆ in. = 1 inch.
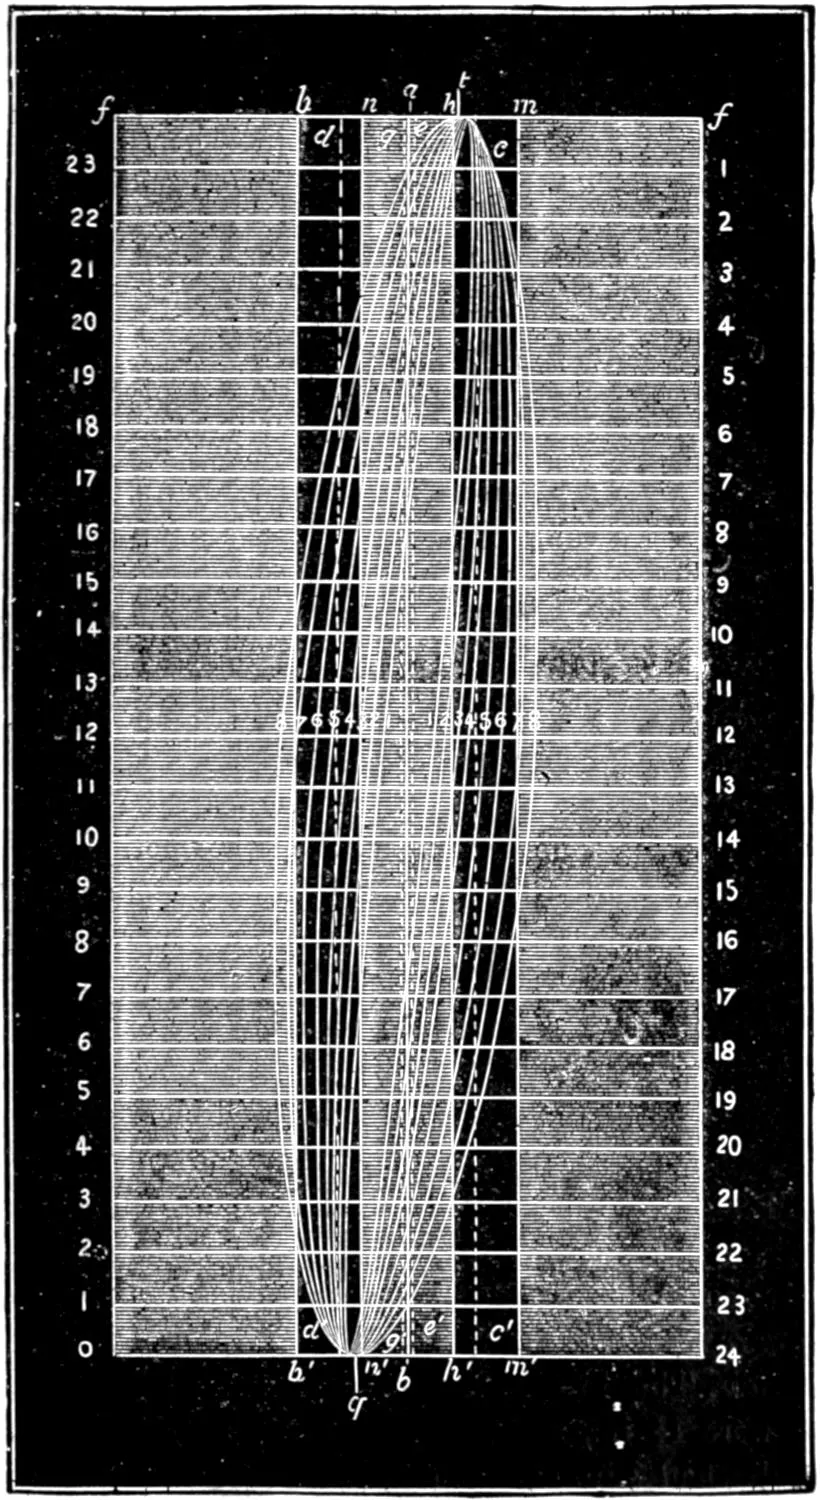
Similar motion-curves, such as h′ i′ j′ k′ l′ m′ n′,
(represented in fig. 25) can be drawn to represent the
position of the other edges of the valve, and also for
the return stroke. The latter are shown in dotted
lines. If we follow the curve h′ i′ j′ k′ l′ m′ n′,
which represents the position of the edge of the valve
h′ which governs the exhaust from the back end of
the cylinder, we see that the port d is opened and
closed to the exhaust simultaneously with the opening
and closing of the port c for the admission of steam to
the front end of the cylinder, and that they both remain
open until the completion of the stroke.
The width that the ports are opened by the valve is
thus ascertainable from these diagrams, for any point
of the stroke, and in fact can be seen at a glance.
By the aid of such motion-curves, the movement of
slide-valves can therefore be analyzed more perfectly
than is possible without them.
Question 45.What were some of the disadvantages
of valves, like that shown in fig. 10, and which are shown
by the motion-curves in fig. 25.
Answer. The free admission of the steam until the
completion of the stroke by the piston was hurtful to
the machinery, as it co-operated with the momentum
of the piston and its connections in producing undue
strains in the working parts. The steam then escaped
from the cylinder without expansion, so that much of
its useful energy was lost. The steam was not allowed
to escape from one end of the cylinder until it
was admitted at the opposite end, and as the process
of exhausting it occupies some time, there was always
more or less back pressure until all the exhaust steam
was expelled from the cylinder. In practice, the imperfections
of the valve-gear frequently delayed the
opening of the ports, both for admitting and exhausting
steam, until after the commencement of the stroke
of the piston.[13]
Question 46.How may some of these evils be overcome?
Answer. By moving the eccentric forward on the
axle so that the motion of the valve is advanced to the
same extent, and the admission and exhaust of the
steam will occur a little before the completion of the
stroke of the piston. In this way the steam is admitted
into the cylinder so as to act as a cushion to
receive the momentum of the piston, and some time is
given to the exhaust steam to escape, before the return
stroke.
Question 47.What is meant by lead?
Answer. By lead is meant the width of the opening
of the steam-ports at the beginning of the stroke of
the piston. On the steam side of the valve it is called
outside lead; on the exhaust side inside lead. In fig.
26 the opening h of the steam-port is the outside lead
and h′ the inside lead.
Fig. 26.
Scale ³⁄₁₆ in. = 1 inch.
Question 48.What is meant by the travel of a valve?
Answer. By the travel we mean the motion of the
valve back and forth, or in other words its stroke. If
the arms of the rocker are of the same length, the
travel of the valve is equal to the throw of the eccentric.
For the preceding illustrations we have selected
an eccentric with three inches throw, which is the
travel of the valve.
Fig. 27.
Scale ³⁄₁₆ in. = 1 inch.
Question 49.How is the steam made to work expansively
with a slide-valve?
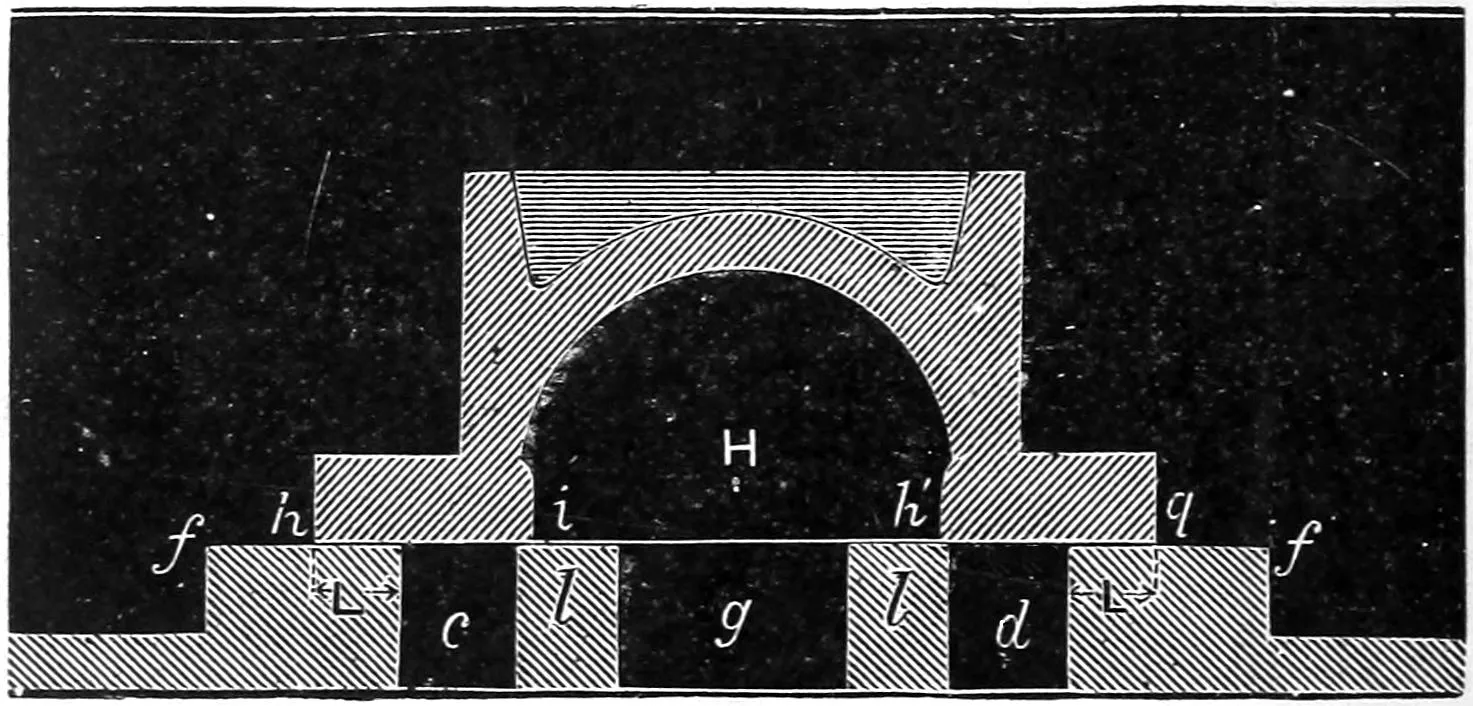
Answer. By giving the valve what is called lap.
That is, by allowing the edges of the valve when it is
in the center of the valve-seat to overlap the edges of
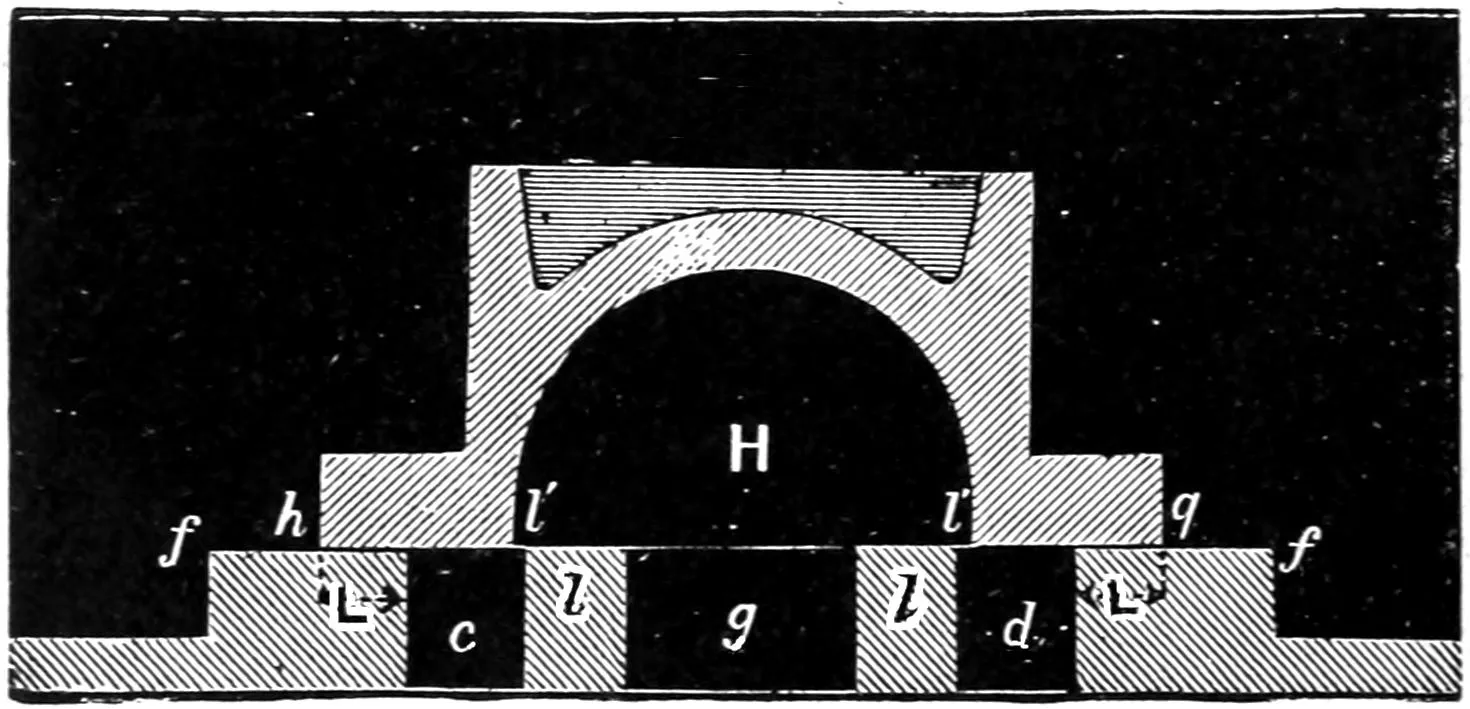
the steam-ports, as shown in fig. 27. Where this overlap,
L L, is on the outside of the valve, it is called
outside lap; when on the inside, l l, inside lap. When
a valve has lap, those portions of the face[14]h, i, and
h′, q, which cover the steam-ports, being wider than
the ports, therefore occupy some time in moving over
them, during which time the steam is enclosed in the
end of the cylinder, as there is then no communication
either with the steam-chest or the exhaust-port. This
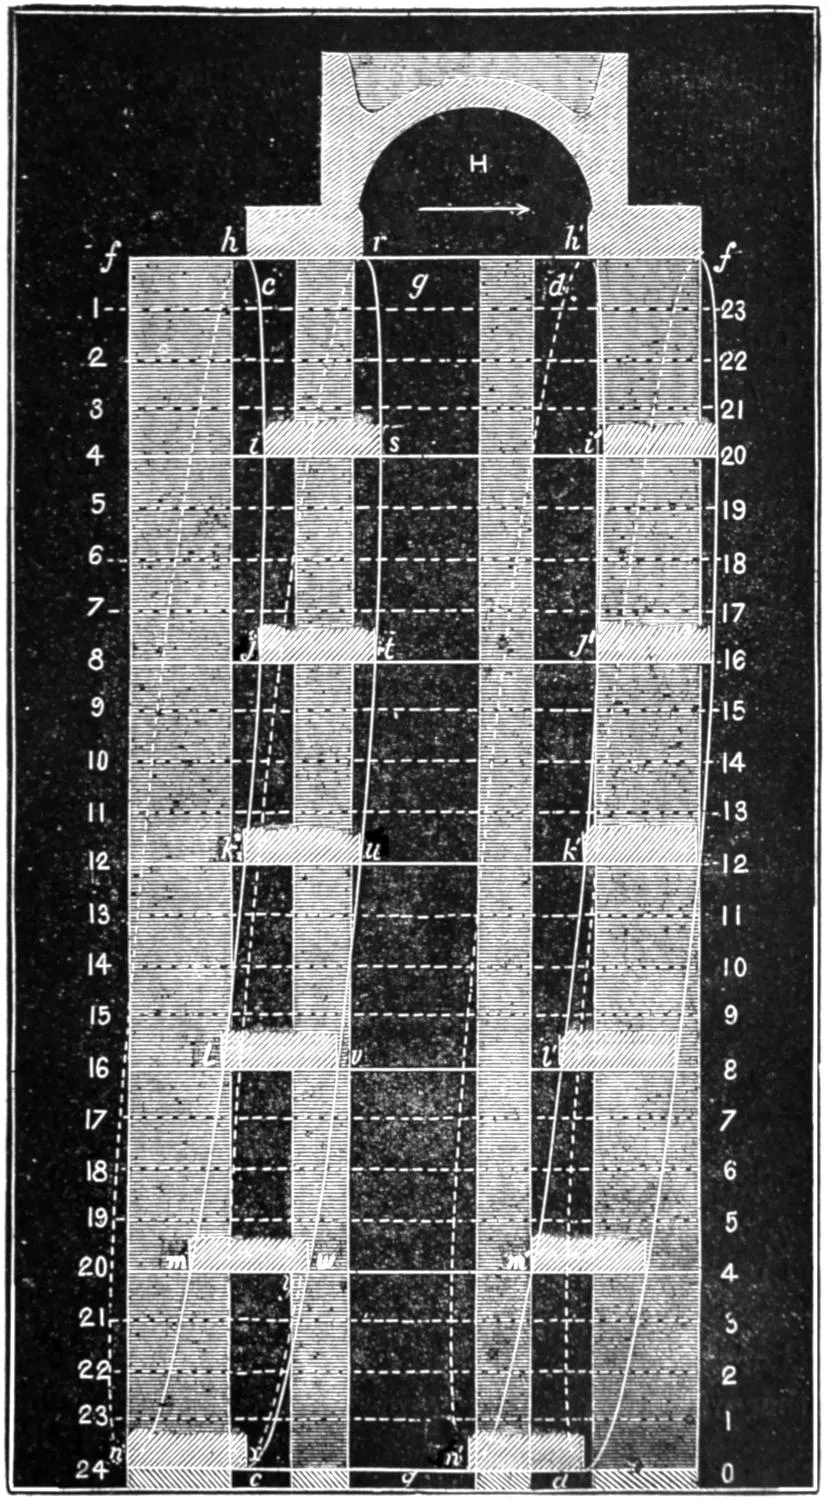
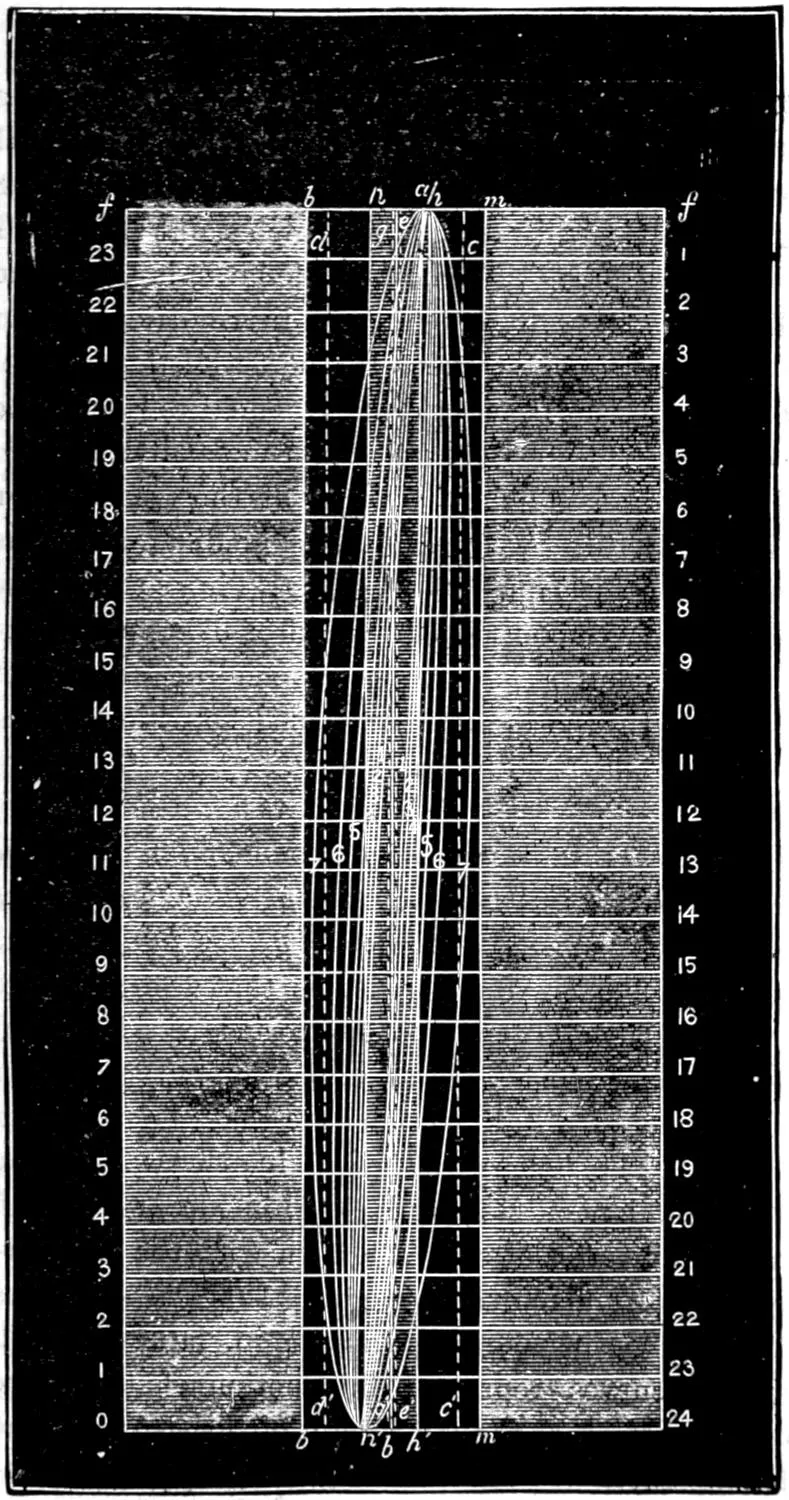
action is shown very clearly by the motion-curves in
fig. 26. The valve in this case has ¹⁄₄ inch lead. At
4¹⁄₂ inches of the stroke of the piston the valve has
moved as far as it will go in that direction, and the
steam-port has its maximum width of opening. From
that point the valve will begin to close the steam-port,
and at 14¹⁄₂ inches of the stroke the port will be
entirely covered, and the steam therefore be cut off.
The port will remain closed until the piston has
moved 21³⁄₄ inches, when it will be observed from the
motion-curve r s t u v w x, that the port c is opened
to the exhaust and the steam escapes, or, as it is technically
called, the release takes place. From the time
the steam is cut off to the time it is released, it works
expansively in the cylinder.
[14] The valve-face is the surface of the valve in contact with the valve-seat.
Question 50.What relation is there between the
amount of lap[15]and the degree of expansion?
[15] In speaking simply of lap, outside lap is always meant.
Answer. The greater the lap with any given travel,
the shorter will be the period of admission of steam,
and, consequently, the more time and space for expansion.
Question 51.What is the effect of inside lap?
Answer. It delays the release of the steam. Thus
in fig. 26 the valve has ¹⁄₈ in. inside lap. The motion-curve
r s t u v w x shows that the release takes
place during the back stroke at 21³⁄₄ in. If now there
was no inside lap, the dotted line y, x would represent
the exhaust edges of the valve, and the release would
then occur somewhat earlier, or at 21 in. For this
reason no inside lap is usually given to valves for engines
which run at high rates of speed, as it allows
too little time for the steam to escape. In fact, in
some cases, what is called inside clearance is given to
the valve; that is, the valve as shown in fig. 29, when
it is in the middle of the valve-face, does not entirely
cover the steam-ports. The effect of this is just the
reverse of that produced by inside lap; that is, it
causes the release to occur earlier in the stroke.
Fig. 29.
Scale ³⁄₁₆ in. = 1 inch.
Question 52.With the same outside lap, what is the
effect of changing the travel of the valve?
Answer. By increasing the travel, the period of admission
is increased and that for expansion lessened;
and by reducing it, the admission is lessened, and the
degree of expansion is increased. This is shown by
the motion-curves in fig. 28, in which the same valve
and ports are represented as are shown in fig. 26, but
the valve has a travel of 5 instead of 3 inches. The
valve also has the same lead. By following the motion-curve
h i j k l m n, it will be seen that the
steam is thus admitted up to 20¹⁄₂ inches of the stroke
of the piston, and the period of expansion, as compared
with that in fig. 26, is correspondingly lessened.
It will also be seen by comparing fig. 26 with fig. 28
that with the short travel of the valve the ports are
not opened so wide as they are when the travel is increased.
This evil is practically obviated, however,
by making the ports so long that with a comparatively
small opening they will still have area sufficient
to admit enough steam to fill the cylinders, and it is
known that an opening less than the whole area of the
steam-ports is sufficient to facilitate the passage of
steam into the cylinder.
Fig. 28.
Scale ³⁄₁₆ in. = 1 inch.
Question 53.How is the exhaust affected by lap and
lead?
Answer. The steam is released earlier in the stroke
in proportion as the amount of outside lap and lead is
increased, but the steam-port is also closed to the exhaust,
or compression, as it is called, begins earlier with
lap and lead than without. Thus, in fig. 25, it will be
seen that at the beginning of the stroke both ports
are entirely closed; in fig. 26, however, in which the
valve has both lap and lead, the port d is nearly wide
open at the beginning of the stroke, and by following
the motion-curve r s t u v w x, which represents
the position of the exhaust edge of the valve, it will
be seen that the steam was released from the port c
before the piston had completed its stroke, or when it
had still nearly 3¹⁄₂ inches to move. In fig. 25 the port
c is not opened to the exhaust until the commencement
of the stroke, but it remains open to its completion,
whereas in fig. 26 it is closed, or compression
begins, at 18 inches of the return stroke, as shown by
the dotted motion-curve.
Question 54.How does the action of the connecting-rod
influence the motion of the valve in relation to the
piston?
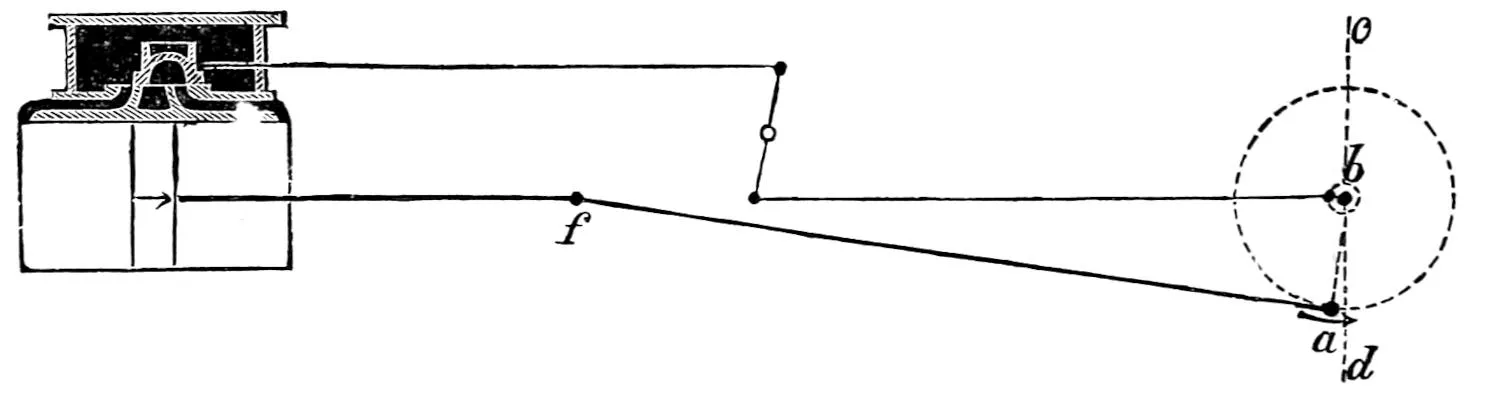
Answer. By delaying the movement of the crank in
the backward stroke of the piston, and accelerating it
in the forward stroke. This will be best explained by
reference to fig. 14, in which the piston is represented
in the center of the cylinder, or the middle of the
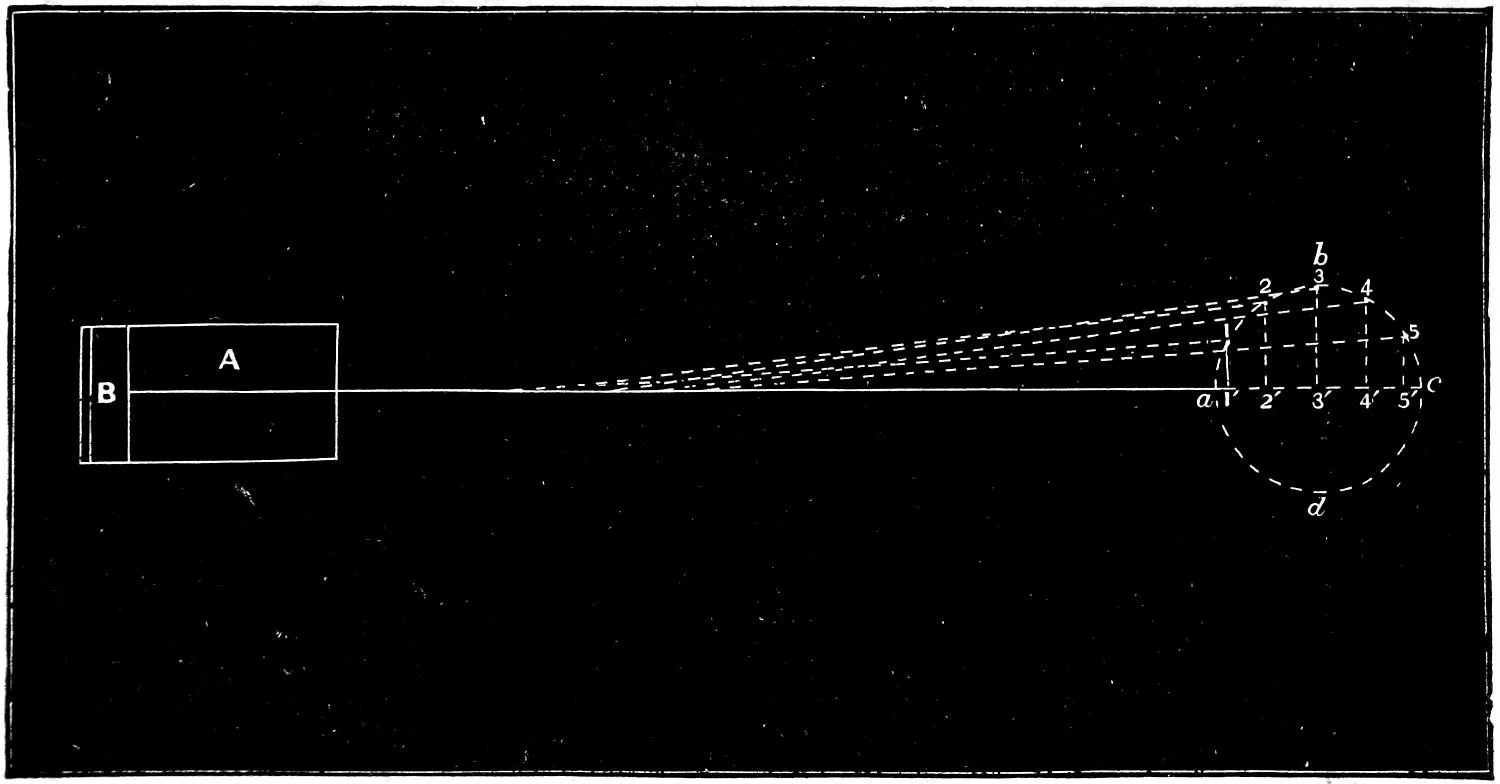
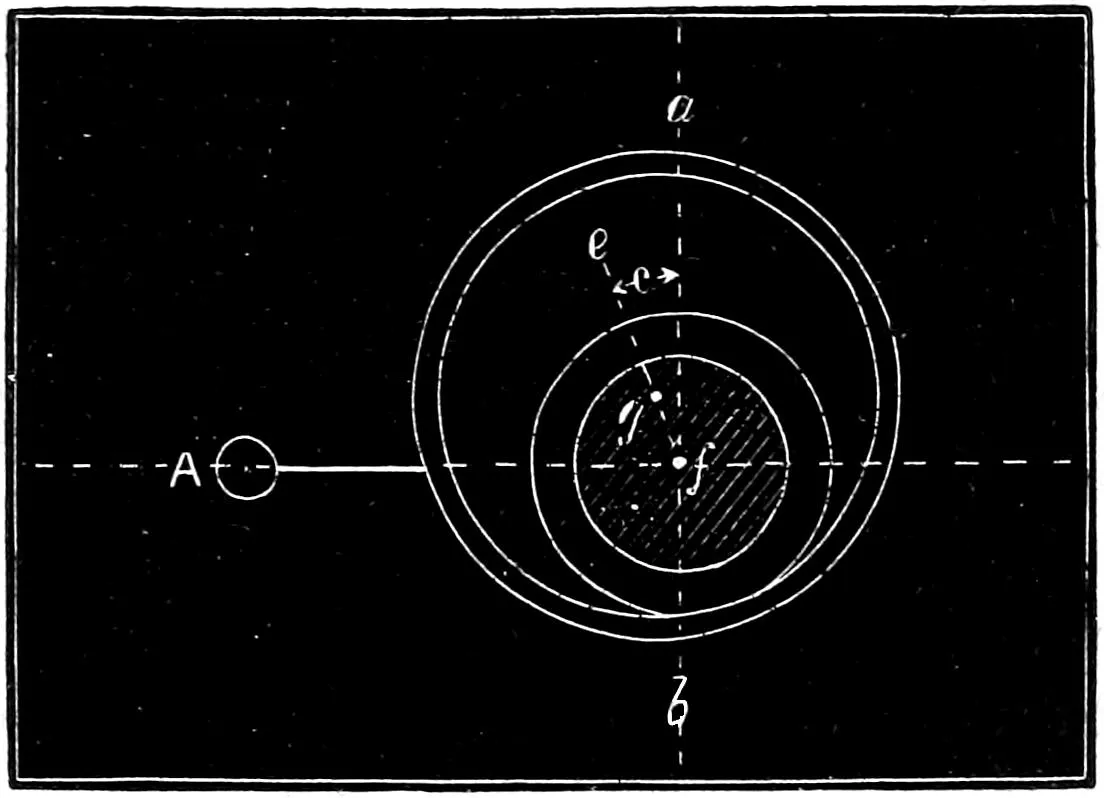
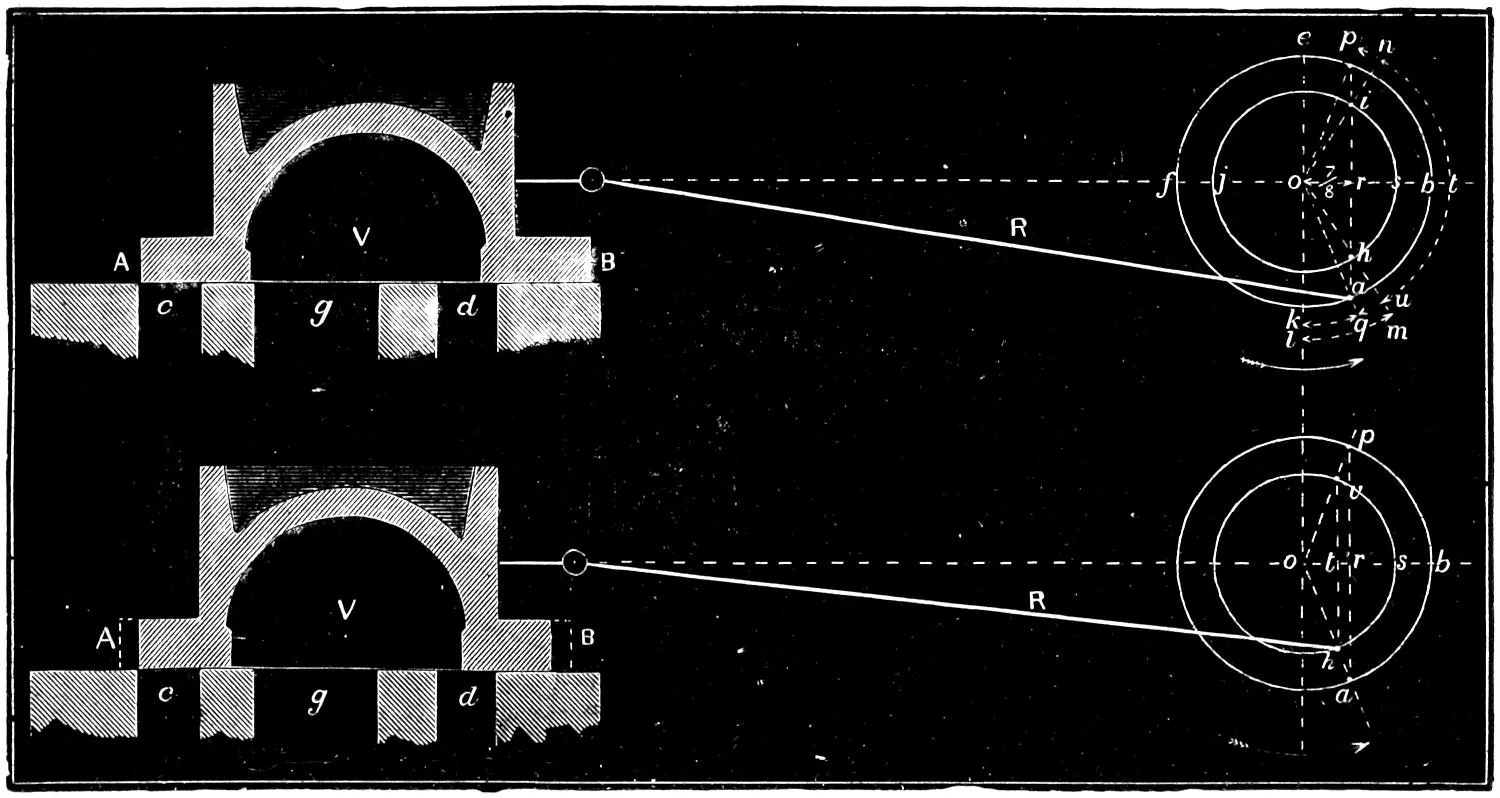
backward stroke. If now we take a pair of dividers
set to a length equal to that of the connecting-rod,
and from the center, f, describe an arc of a circle, a b,
from the center of the shaft, and through the lower
half of the circle which represents the path of the
crank-pin, we will find that the point of intersection,
a, falls short of the vertical line, c d, and that the
crank-pin has not made quite one-quarter of a revolution
while the piston was moving through the first
half of the backward stroke. By referring to fig. 21,
in which the piston is again in the middle of its stroke,
but is moving forward, and by describing another arc
of a circle, b a, from the center of the shaft and intersecting
the path of the crank-pin, it will be seen that
the latter has moved more than a quarter revolution,
while the piston has made the first half of the forward
stroke. Owing to this angularity, as it is called, of
the connecting-rod, the crank-pin is behind the piston
during its backward stroke and ahead of it during the
forward stroke. As the valve is moved by the eccentric,
and it in turn by the shaft and crank, any irregularities
of the latter are of course communicated to
the valve. We therefore find, by referring to fig. 26,
that the point of cut-off occurs during the backward
stroke at 14¹⁄₂ inches, and during the forward stroke at
12 inches. A similar inequality is observable in the
points of release for the front and back strokes. It is
not, however, a matter of very great practical importance
with stationary engines which run at comparatively
slow speeds; but if it is thought desirable, the
period of admission and the point of release for both
strokes can be equalized, either by giving the valve
more lead or lap at one end than the other, or by
making the one steam-port wider than the other. The
mechanism employed for moving locomotive slide-valves,
however, furnishes us with the means of modifying
their motion in relation to that of the piston,
and of thus equalizing the periods of admission and
release for the front and back strokes. The methods
of doing this will be more fully explained hereafter.
PART V. THE EXPANSION OF STEAM.
Fig. 30.
Scale ²⁄₃ in. = 1 foot.
Fig. 31.
Scale ¹⁄₄ in. = 1 inch.
Question 55.How can we determine by experiment
the pressure of the steam in the cylinder at all points of
the stroke?
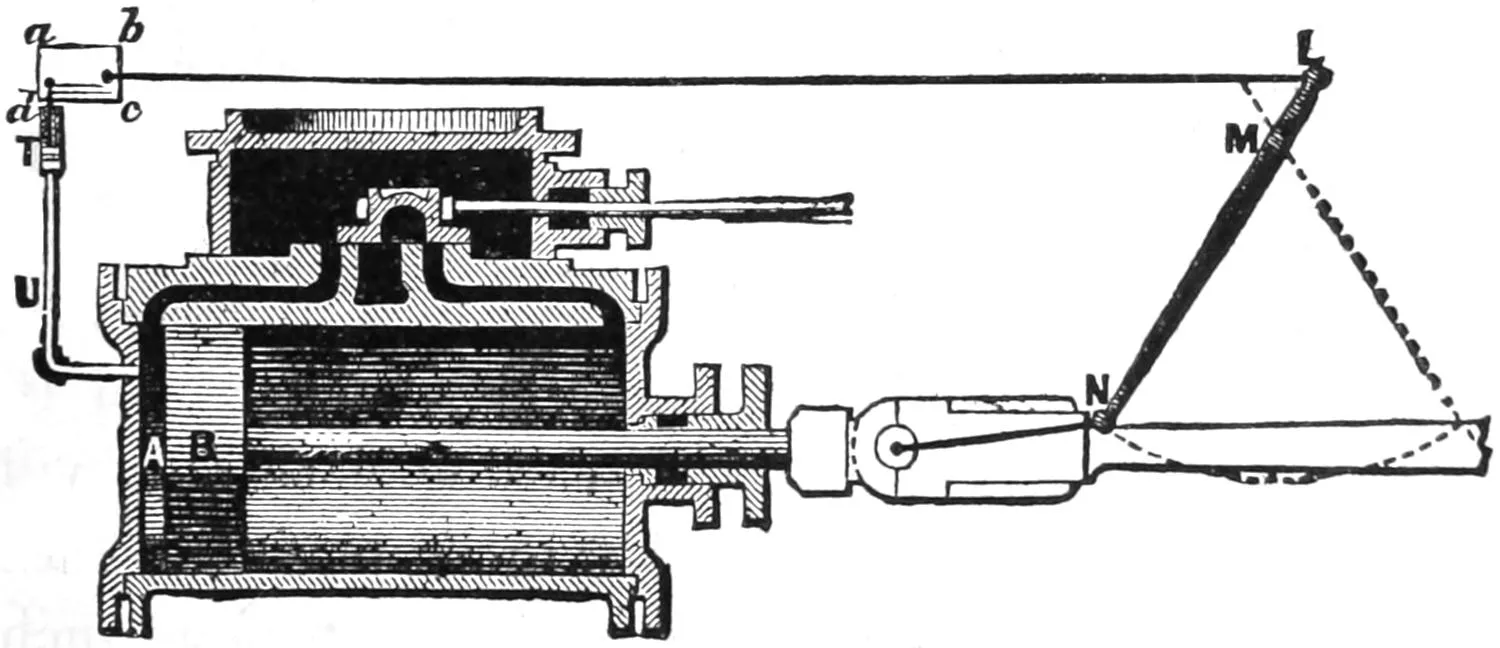
Answer. By the use of an instrument made for that
purpose, called an indicator. Its action can be best explained
by supposing that we have a small cylinder and
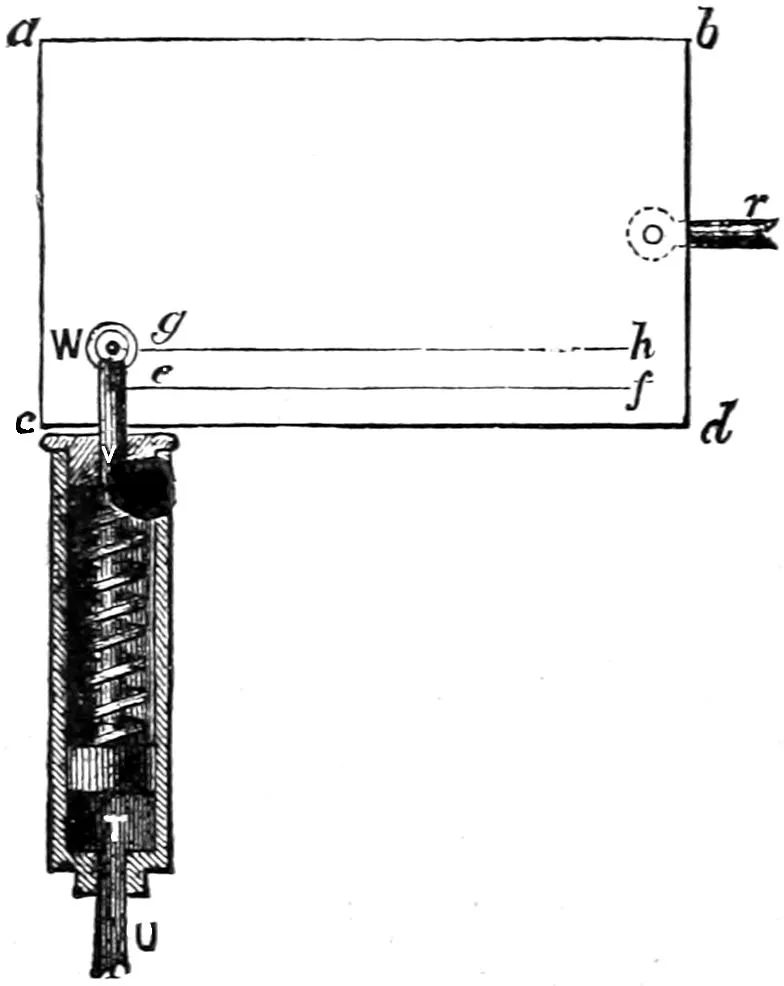
piston, T, fig. 30, (shown on an enlarged scale in fig. 31)
attached by a pipe U to one end of the cylinder A, so
that when steam is admitted to the latter it will be
conducted to the small cylinder T through the pipe U.
Over the small piston and attached to it is a spiral
spring, s s, fig. 31, which is compressed when the piston
rises and extended when it falls. To the top of
the piston-rod, V, a pencil, W, is attached. Behind
this pencil we will suppose there is a card, a b c d,
and that this card is so arranged that we can slide
it horizontally and in contact with the pencil point.
With only the pressure of the atmosphere above and
below the piston T, the spring would be neither compressed
nor extended, and the piston would then stand
in the position shown in fig. 31. If now we move
card horizontally, the pencil will draw a line, g, h,
called the atmospheric line. We will now suppose that
the tension of the spring is such that a pressure of 10
lbs. per square inch above or below the piston will
either extend or compress the spring ¹⁄₄ inch. In
other words, every pound of pressure per square inch
in the piston will move it ¹⁄₄₀ of an inch. If we
could produce a vacuum under the piston, it would be
pressed down by the atmosphere above it ¹⁵⁄₄₀, or ³⁄₈
of an inch. If, when it is thus depressed, we again
slide the card along in contact with the pencil-point,
it will draw another line, e, f, called the vacuum-line.
Assuming that we have drawn these two lines, and
that the piston and card are in the position shown in
figs. 30 and 31, we will then suppose that a reciprocating
motion can be given to the card by the lever
L, M, N, fig. 30, which is pivoted at M and attached
at N to the piston-rod by a short connecting-rod. It
is obvious that by connecting the upper end L of the
lever with a rod, L c, to the card, the latter will be
moved backwards and forwards by the motion of the
piston B, and that the motion of the card will
be simultaneous with that of the piston B, but
of course of shorter stroke. We will assume that
the stroke of the card is equal to the length of the
atmospheric and vacuum lines g h and e f, fig. 31. If
now, the piston being at the beginning of the stroke
as shown in fig. 30, we admit steam of 85 lbs. effective
pressure per square inch (which is equal to
100 lbs. absolute pressure) into the cylinder A, it will
be conveyed through the pipe U to the cylinder
T, and will force up the piston ⁸⁵⁄₄₀ or 2¹⁄₈ inches
above the atmospheric line, or ¹⁰⁰⁄₄₀ or 2¹⁄₂ inches
above the vacuum line, as shown in fig. 32, and the
pencil will draw a vertical line, g i, on the card, (represented
by a dotted line in fig. 32.) We will suppose
that steam is admitted during 8 inches of the
stroke, and is then cut off. When the piston B, fig.
30, has moved that distance, which is one-third of its
stroke, the card will also have moved one-third of its
stroke, and will stand in relation to the pencil in the
position represented in fig. 33, and as the absolute
steam pressure in the cylinder was maintained at 100
lbs. while the card was moving that distance, the pencil
will have drawn a horizontal line, i j. The steam
is now cut off and begins to expand, and its pressure
is thereby reduced. When the piston of the engine is
at half-stroke, the card will also be at half-stroke, and
the steam will be expanded from 8 to 12 inches of the
stroke. By the rule given in the answer to question
20, its absolute pressure would then be 66²⁄₃ lbs., and
the indicator-piston will then be pressed down by the
spring, so that the pencil will stand in the position
shown in fig. 34, or 66²⁄₃ fortieths of an inch above the
atmospheric line. The pencil meanwhile will have
drawn the curved line j k. When the piston has
moved 16 inches, the steam will be expanded to double
its volume and its absolute pressure will therefore be
50 lbs., and consequently the pencil will stand 50 fortieths
or 1¹⁄₄ inch above the atmospheric line as shown
in fig. 35, and the pencil will have continued the curve
j k to l. At 20 inches the steam will have 40 lbs.,
and at the completion of the stroke 33²⁄₃ lbs. absolute
pressure, and the pencil will have completed the curve
j k l m n, as shown in figs. 36 and 37. This curve
is called the expansion curve, and its form is that which
mathematicians call a hyperbolic curve. If the steam
is exhausted, the indicator-piston will descend and
carry the pencil down to the atmospheric line, and the
vertical line n h, fig. 38, will be drawn. On the return
stroke, after the steam is exhausted from the
main cylinder A, fig. 30, the pencil would draw the
atmospheric line g h, fig. 38, thus showing that there
is no steam pressure under the piston. Such a diagram
is called an indicator diagram.[16] In practice
there are a great many influences which modify it,
such as condensation, performance of work, imperfection
of valve gear, etc., but for the present these are
disregarded.
[16] The indicator used in practice, to show the action of the steam in
the cylinders of steam engines, differs essentially in its construction from
that which we have described. The principles of operation are, however,
the same in both. We will explain the construction of the Richard’s
indicator, the one which is now most generally used, hereafter.
Fig. 32.
Fig. 33.
Fig. 34.
Fig. 35.
Fig. 36.
Fig. 37.
Fig. 38.
Scale ¹⁄₄ in. = 1 inch.
Question 56.How can we ascertain the pressure of
the steam for any point of the stroke from such a diagram?
Answer. By measuring the vertical distance by the
expansion curve (fig. 38) from the vacuum or the atmospheric
line, as for example 8 j, 12 k, 16 l, 20 m.
As the indicator spring is extended or compressed one-fortieth
of an inch[17] from every pound of pressure per
square inch, either above or below the indicator piston,
if we construct a scale S, S, fig. 38, with division
of one-fortieth of an inch each, one of them will represent
one pound of pressure per square inch if measured
vertically from the atmospheric or vacuum line.
If we sub-divide the vacuum line with the same number
of parts as there are inches in the stroke of the
piston (see fig. 39) we can draw vertical lines from
these points and thus determine the pressure by comparing
the length of such lines with the scale S, S.
Thus the line 8 j measures 100 fortieths of an inch,
thus showing that the absolute steam pressure at 8
inches of the stroke was 100 lbs. per square inch; the
line 12 k measures 66²⁄₃ fortieths of an inch, thus showing
that at 12 inches of the stroke the steam pressure
was 66²⁄₃ lbs. At 16, 20 and 24 inches of the stroke
the vertical lines measure 50, 40 and 33²⁄₃ fortieths;
and therefore there were that number of pounds of
steam pressure when the piston was at the point of the
stroke named. Similar measurements could be made
from other points, such as 2, 6, 10, or any other number
of inches of the stroke. Of course, if we measure
from the vacuum line we will have the absolute steam
pressure, or the pressure above a vacuum, as it is sometimes
called; if we measure from the atmospheric line
we will have the effective pressure, or the pressure
above the atmosphere.
[17] Indicator springs are used of various degrees of tension, in proportion
to the steam pressure to be indicated.
Fig. 39.
Scale ¹⁄₄ in. = 1 inch.
Question 57.How can we determine the average
pressure during the whole stroke of steam which works expansively?
Answer. This can be determined approximately by
the following method: In the first place, divide the
vacuum line (fig. 39) into any number of equal divisions,
say six. From the points of division, 4, 8, 12,
16 and 20, which in this case correspond with the
points which represent inches of the stroke, draw perpendicular
lines, which will divide the indicator diagram
into six divisions. It is obvious that during the
time the steam is working full stroke the pressure is
uniformly 100 lbs. absolute. While the piston is moving
from 8 to 12 inches the pressure falls from 100 to
66²⁄₃ lbs., so that at 10 inches we have very nearly the
average pressure during the period named. So from
12 to 16, 16 to 20 and 20 to 24 the average is nearly
57.1, 44.4 and 36.3 lbs., respectively. Now, by adding
together the pressures in the middle of
each one of a number of equal divisions of
the stroke and dividing by the number of
divisions, we will obtain approximately the
average absolute pressure during the whole
stroke. To get the average effective pressure,
deduct the atmospheric pressure from
the result. The calculation would in the above
case be as follows:
100
lbs.
100
„
80
„
57
.1
44
.4
36
.3
6)417
.8
69
.6
= Average absolute pressure.
15
54
.6
= Average effective pressure.
A more accurate way of calculating the average or
mean pressure, as it is called, when steam is used expansively,
and the one which is usually employed, is to
divide the length of the piston’s stroke in
inches by the number of inches at which the
steam is cut off: the quotient is the ratio
of expansion. Get the Hyperbolic Logarithm
of the ratio of expansion from the table of
logarithms in the appendix, add 1 to it, and
divide the sum by the ratio of expansion and
multiply the quotient by the mean absolute
steam pressure in the cylinder during its admission.
The result will be the mean absolute
pressure during the stroke. To get the
mean effective pressure, deduct the atmospheric
pressure.
The calculation for the above example would be
as follows:
The table of hyperbolic logarithms given in the
appendix will be needed in calculating the mean pressure
of steam used expansively:
Question 58.What advantages result from using
steam expansively?
Answer. There is a very important saving in the
amount of steam required to do a given amount of
work, and the strains and shocks which are produced
by the rapid motion of the piston and other reciprocating
and revolving parts of the engine are very
much diminished by allowing the steam to expand,
and thus become reduced in pressure during the latter
part of the stroke.
Question 59.How is steam saved by using it expansively?
Answer. Less steam is required when it is used expansively:
1. Because when steam of a high pressure is introduced
into the cylinder, and allowed to expand until
its pressure is comparatively low, it escapes at a
lower pressure than the average pressure during the
whole stroke. If steam of a pressure equal to the
average pressure is worked full stroke, it would exert
exactly the same force on the piston as the steam of
higher pressure did when working expansively, but
the pressure in the latter case, when the piston reaches
the end of the stroke, or the final pressure, as it is
called, would be considerably lower than in the other.
The pressure of steam represents energy, or capacity for
doing work, and therefore if we allow it to escape with
a comparatively high pressure without doing work, it
is a waste of energy. To illustrate this, we will take
the same conditions which were used in the answer to
Question 57, in calculating the average pressure. In
that case the mean absolute pressure of the steam was
69.95 pounds per square inch, but the pressure at the
end of the stroke, when the steam escaped, was only 33²⁄₃
pounds absolute. If, therefore, steam had been used
of the average pressure through the whole stroke, it
would have escaped with a pressure of 69.95 pounds,
or more than twice that of the expanded steam, and
the work done in both cases would have been the
same.
2. There is also another incidental advantage in
this, because low-pressure steam can be exhausted
more quickly from a cylinder than steam of a high
pressure, and consequently there is less resistance, or
back pressure, as it is called, in the exhausted end of
the cylinder to the movement of the piston.
3. The causes which produce the greatest economy
when steam is used expansively cannot be fully explained
without discussing principles of science more
abstruse than it is desirable to introduce here. They
can, however, with the aid of the table of the “Properties
of Steam,”[18] in the appendix, be illustrated by a
few simple calculations, so that the economy of using
steam expansively will be apparent.
[18] This table is copied from Colburn’s Treatise on the Locomotive
Engine.
For the basis of the calculations the same data and
dimensions will be employed that were used in the
previous illustration; that is, a cylinder of 16 in. diameter
and piston with 24 in. stroke and steam of
100 lbs. absolute pressure cut off at 8 in. of the stroke.
We will suppose, further, that the steam used is generated
from water of a temperature of 60 degrees, and
we will then calculate the total number of units of heat
in the steam used for each stroke of the piston. The
area of a piston 16 in. in diameter is 201 square
inches; and as the steam is admitted until the piston
moves 8 inches of its stroke, therefore the quantity of
steam would be 8 times 201 cubic inches, or
201 × 8 = 1608 cubic in. =
16081728 cubic ft.
From the table it will be seen that one cubic foot of
steam of 100 lbs. pressure weighs .2307 lbs.; therefore
the weight of the fraction of a cubic foot given
above would be calculated as follows:
.2307 × 16081728 = .2146 lb.
= weight of 1608 cubic in. of
steam of 100 lbs. absolute pressure.
From the table it will be seen that the total heat
above zero of steam of 100 lbs. absolute pressure is
1213.4 degrees. That is, as was explained in answer
to Question 40,[19] in order to boil water under a pressure
of 100 lbs. per square inch we must first heat
water up to 327.9 degrees, and then, to convert it into
steam, 885.5 degrees more must be added. It was
also explained in the answer to Question 35 that one
pound of water heated one degree is the standard of
measurement or unit of heat. Now if we have 1 lb. of
water with a temperature of zero, evidently it will
take 1213.4 units of heat to convert it into steam of
100 lbs. absolute pressure. But as the water from
which our steam was generated had a temperature of
60 degrees, we must deduct that much from 1213.4:
1213.4 - 60 = 1153.4 = units of heat in one pound of
steam of 100 lbs. absolute pressure generated from
water of 60 degrees temperature.
[19] In the illustration used in
answer to Question 40, steam of 100 lbs.
effective pressure was used, whereas in the above case it is absolute
pressure.
If now one pound of steam has 1153.4 units of heat,
the following calculation will give the units of heat in
.2146 lbs.: 1153.4 × .2146 = 247.51 = units of heat in
.2146 lbs., or 1608 cubic in. of steam of 100 lbs. absolute
pressure.
It was shown in answer to Question 57 that the
average pressure of steam of 100 lbs. cut off at 8
in. of the stroke was 69.95 lbs. per square inch. Disregarding
the small fraction, we will call it 70 lbs.
Now if we admit steam of this pressure through the
whole stroke of the piston, we will use 4,824 cubic inches.
It will be found by a calculation similar to the above,
that to generate this quantity of steam of 70 lbs.
pressure from water of a temperature of 60 degrees
would require 527 units of heat, or more than twice as
many as were required to do the same work with steam
of 100 lbs. pressure cut off at 8 inches when using
it expansively during the rest of the stroke. The actual
difference in practice is not so great as this, because
the loss of heat from radiation and condensation
in the cylinder and other causes is greater when steam
of a high pressure is expanded than when lower
pressure steam is admitted through the whole stroke.
But after allowance is made for all such sources of
loss and waste, there is still an enormous gain from
using steam expansively.
Question 60.What is meant by wire-drawn steam?
Answer. It is the fall which the pressure of the
steam undergoes during its passage from the boiler to
the cylinder,[20] and which is due to the contracted
opening of the steam pipes or valves.
Question 61.What is the economical effect of reducing
the pressure, or of wire-drawing it, by partly
closing the valve by which it is admitted to the cylinders?
Answer. By reducing the pressure of steam in this
or any other way, it is necessary in doing the same
amount of work to admit steam to the cylinder for a
longer period, and therefore to reduce the degree of
expansion. To illustrate the effect of this, we will
estimate the total heat required to exert a pressure of
70 lbs. on the piston described above. It will be assumed
that the steam pressure in the boiler is 100 lbs.
absolute, and that this is wire-drawn down to 70 lbs.
and admitted to the cylinder through the whole stroke.
As was shown in the preceding answer, 4,824 cubic
inches of steam are required to fill the cylinder. Now
3,376.8 cubic inches of steam of 100 lbs. pressure, if
expanded to 70 lbs. pressure, will make 4,824 cubic
inches. The total heat required to generate 3,376.8
cubic inches of steam of 100 lbs. absolute pressure
from water of 60 degrees is 519.9 units, so that to do
the same work by using steam of high pressure cut off
at one-third of the stroke, using steam of low boiler
pressure full stroke, and using wire-drawn steam full
stroke, would, in the example we have selected, require
247.5, 527 and 519.9 units of heat respectively.
Question 62.To what extent can we work steam expansively,
with advantage and economy?
Answer. The theoretical economy of using steam increases
with the degree of expansion and the pressure.
This is shown very clearly in the following table, in
the first column of which the number of inches of the
piston stroke is given during which steam is admitted
to a cylinder 16 in. in diameter and 24 in. stroke. In
the second column is given the pressure of the steam,
or initial pressure, as it is called, which must be admitted
into the cylinder in order to produce a mean
pressure of 70 lbs. per square inch when it is cut off
at the point indicated in the first column. In the
third column is given the total heat which is required
to generate the steam required in each case, and in
the last column the percentage of saving is given
which results from the different degrees of expansion
and a mean pressure of 70 lbs. per square inch in each
case.
RESULTS OF USING STEAM EXPANSIVELY.
Period of admission or point of cut-off.
Initial Pressure of steam in pounds per square inch.
Total heat of steam used, in units.
Percentage of saving compared with full stroke.
Full stroke
70
.
527
.
18 in. = Three-quarters of the stroke,
72
.5
408
.7
22
¹⁄₂
12 in. = One-half„„
82
.7
309
.5
41
¹⁄₄
8 in. = One-third„„
100
.
247
.5
53
6 in. = One-quarter„„
117
.4
215
.9
58
4 in. = One-sixth„„
150
.5
186
.5
64
¹⁄₂
3 in. = One-eighth„„
181
.8
165
.8
68
¹⁄₂
2 in. = One-twelfth„„
241
.4
144
.8
72
¹⁄₂
From this table it will be seen that theoretically
22¹⁄₂ per cent. of heat is saved by cutting off at ³⁄₄ of
the stroke and using steam of 72.5 lbs. pressure instead
of steam of 70 lbs. worked full stroke. Cutting
off at half stroke and using steam of 82.7 lbs., 41¹⁄₄ per
cent. of heat is saved, and cutting off at quarter
stroke with steam of 117.4 lbs. saves 58 per cent. of
heat; and at one-twelfth of the stroke, or expanding
steam of 241.4 lbs. pressure to twelve times its volume,
saves 72¹⁄₂ per cent. of heat.
As stated before, the above is the theoretical advantage
of using steam expansively. There are, however,
practical difficulties in the way of using some of these
high degrees of expansion. It has already been explained
that if steam is cut off early in the stroke and
the degree of expansion increased, the pressure and
consequently the temperature of the steam must also
be increased. The danger of explosion is greater with
the higher pressures, and stronger and more expensive
boilers and machinery are therefore needed. With
steam of very high temperature the metal of the cylinders,
pistons and valves becomes so much heated
that they soften, and then the friction of the one on
the other causes them to cut or scratch each other.
The high temperature at the same time destroys the
oil or other lubricant used in contact with the steam.
It is also impossible to admit and cut off steam very
early in the stroke with the ordinary mechanical appliances
used for moving slide-valves of locomotives.
This latter difficulty will be more fully explained hereafter.
PART VI. GENERAL DESCRIPTION OF A LOCOMOTIVE ENGINE.
Question 63.What are the principal parts of an ordinary
locomotive engine?
Answer. A boiler for generating steam and a pair of
high-pressure steam engines, which are all mounted
on a suitable frame and wheels adapted for running
on a track consisting of two iron or steel rails.
Question 64.How is the power of high-pressure engines
applied to locomotives?
Answer. By connecting the engines with the wheels
so as to give the latter a rotary motion.
Question 65.When they revolve what will occur?
Answer. Either they will slip on the track, or the
locomotive will move either backward or forward, according
to the direction the wheels are turning.
Question 66.What will determine whether the wheels
will slip or the locomotive move?
Answer. The friction or adhesion, as it is called, between
the wheels and the track. If this adhesion is
greater than the resistance opposed to the movement
of the locomotive, the latter will overcome the resistance;
but if the latter is greater than the friction,
the wheels will slip.
Question 67.Upon what does the amount of friction
or adhesion of the wheels depend?
Answer. Chiefly on the weight which they bear,
but to some extent upon the condition of the rails.
Under ordinary circumstances, the adhesion of the
wheels of a locomotive is in direct proportion to the
weight they carry.
Question 68.Why are two cylinders employed on locomotives?
Answer. Because if only one was used, it would be
impossible or very difficult to start the engine, if it
should stop on one of the dead points.
Question 69.How is this difficulty overcome by the
use of two cylinders?
Answer. By attaching the two cranks to the same
shaft or axle, and placing them at right angles to each
other, so that when the one is at a dead point the
other is in the position where the steam can exert the
maximum power on the crank.
Question 70.How are the cranks of an ordinary locomotive
made?
Answer. They are cast in one piece with the wheels
that drive the locomotive, which are therefore called
driving-wheels. In this country the centre portion of
such wheels, or wheel-centres as they are called, is always
made of cast iron, with tires of wrought iron or
steel around the outside, and is fastened to the axles
of the locomotive. The shaft of a locomotive engine
is called the main driving-axle, and the wheels attached
to it the main driving-wheels.
Question 71.How are the cylinders and driving-wheels
of a locomotive usually placed?
Answer. The cylinders A, plates I, II and III, are
placed at the front end of the locomotive, and the
main driving-axle, B, far enough behind them to permit
the connecting rods, C, to be attached to pins, D,
in the cranks, called crank-pins. In this country
these cranks are now universally placed on the outside
of the wheels, and therefore the cylinders must be
placed far enough apart (as shown in fig. 40 and Plate
III) to permit the connecting-rods to be attached to the
crank-pins. The cylinders are therefore placed outside
the frames, H, H, Plate III, (the latter are inside
of the wheels,) and are now nearly always horizontal,
although in old engines they are often inclined. Plate
I is a side view of an ordinary eight-wheeled American
locomotive, Plate II a longitudinal section, Plate
III a plan, and fig. 40, a transverse section through
the cylinder and smoke-box.
Fig. 40.
Scale ¹⁄₄ in. = 1 foot.
Question 72.What are the smaller wheels, E E,
called, and what are they for?
Answer. They are called truck-wheels and carry the
weight of the cylinders and other parts of the front
end of the locomotive, and serve to guide and steady
the machine in a manner which will be more fully explained
hereafter.
Question 73.Why are more than one pair of driving
wheels necessary for locomotives?
Answer. Because if all the weight which is needed
to create the requisite adhesion of the wheels of locomotives
to pull heavy loads was placed on one pair of
wheels, it would be so excessive as to partly crush and
injure the rails. It is therefore distributed, usually
on two pairs, but sometimes on three or four or even
more pairs.
Question 74.Where is the second pair of driving-wheels
usually placed?
Answer. These wheels, F—called the back or trailing
driving-wheels—are, in the ordinary type of locomotives
used in this country, situated behind the main
driving-wheels, far enough back to give the room
necessary for the boiler, G, between the two axles, as
shown in plates I, II and III.
Question 75.How are the axles, cylinders, etc., held
in the right position in relation to each other?
Answer. By longitudinal frames, H, H, H, H, which
hold the axles in the proper position, and are bolted to
the cylinders, and also fastened to the boiler at I, I,
Plate I.
Question 76.How is a locomotive engine made to
run either backward or forward?
Answer. By having two eccentrics, J, J, Plate III
(also shown in Plate II,) for each cylinder. One of
these is fixed or set on the shaft in such a position as
to move the valve so that the engine will run in one
direction; the other eccentric is set so that the engine
will run the reverse way. The ends of the two eccentric
rods are attached to what is called a link, L, (Plates
II and III,) the object of which is to furnish the
means of quickly engaging and disengaging either eccentric
rod to or from the rocker, K. The link is
operated by a system of levers, consisting of the lifting
shaft, M, and arms, N, N, and the reverse lever, O, O,
(Plate II). The principles and working of these will
be more fully explained hereafter.
Question 77.What are the principal parts or “organs”
of a locomotive boiler?
Answer. 1. A fire-place, or, as it is called a fire-box,
G, (Plate II,) which is surrounded with water.
2. A cylindrical part, P P, (Plates I and II,) attached
to the fire-box at one end and to a chamber, Q,
called the smoke-box, at the other.
3. The tubes or flues a a′, (Plate II and fig. 40,)
which connect the fire-box with the smoke-box and
pass through the cylindrical part of the boiler and are
surrounded with water.
4. The smoke-stack or chimney R R.
Question 78.What is each of these parts or organs
for and of what do they consist?
Answer. The fire-box G furnishes the room for
burning the fuel, and consists of an inner and outer
shell made of boiler plate, with the space between
the two filled with water; a grate, b b, (Plate II,)
formed of cast-iron bars, with spaces between them
for admitting air for the combustion of the fuel,
which is placed on the top of them; a door, C, called
the furnace-door, for supplying the grate with fuel; a
receptacle, d d, below the grate, to collect ashes, and
therefore called the ash-pan, which is supplied with
suitable dampers, n′, n′, for admitting or excluding the
air from the fire.
The cylindrical part P P, or waist of the boiler as
it is sometimes called, contains the greater part of the
water to be heated.
The flues or tubes, as they are generally called, of
which a locomotive has from one to two hundred, are
usually two inches in diameter, and about eleven feet
long. They conduct the smoke and products of combustion
from the fire-box to the smoke-box. These
tubes are made of small diameter so as to sub-divide
the smoke into many small streams and thus expose
it to a large radiating surface through which the heat
is conducted to the water.
The smoke-stack serves partly for removing into the
open air the smoke which passes through the flues, and
partly for producing a strong draft of air, which is
indispensably necessary for the rapid combustion of
the fuel, and also for collecting and extinguishing
the sparks from the fire.
Question 79.How is the draft produced in locomotive
boilers?
Answer. By conducting the exhaust steam through
pipes (e, e, fig. 40) from the cylinders to the smoke-box
and allowing it to escape up the smoke-stack from
apertures, f, f, (Plate II, fig. 40.) called exhaust nozzles.
The strong current of steam thus produced in the
smoke-stack produces a vacuum, by which the smoke
is sucked into the smoke-box with great power and
forced out of the smoke-stack into the open air.
Question 80.How are the water and fuel carried
which must be supplied to a locomotive while it is running?
Answer. The water is carried in a tank, which is
constructed in the form of the letter U, so as to give
room for the stowage of fuel between its two branches
or sides. This tank is carried on a set of wheels, and
forms a separate vehicle, independent of the locomotive,
called a tender, the construction of which will be
explained in a future chapter.
Question 81.What are the dimensions of the principal
parts of a locomotive?
Answer. There is a great variety in the plan, size
and capacity of locomotives, but the type which is
more generally used in this country than any other,
and which has been selected for the preceding illustrations,
and will be described in the succeeding
chapters of the Catechism, has four driving and four
truck wheels, and weighs in working condition about
60,000 lbs. The following are the dimensions of its
principal parts: The driving-wheels are about 5 feet
and the truck-wheels from 26 to 30 inches in diameter.
The longitudinal distance between the centres
of the driving-wheels is usually about 7 feet, and
between the centres of the truck-wheels 5 ft. 9 in., and
the total distance from the centre of the back driving-wheels
to the centre of the front truck-wheels, which
is called the wheel-base, is 21 ft. 8 in. The weight on
each driving-wheel is usually about 10,000 lbs., and on
each truck-wheel about 5,000 lbs. The cylinders are
16 in. in diameter and the piston has 24 in. stroke,
and the connecting-rod is 7 ft. long measured between
the centres of the pins to which it is attached. The
centres of the cylinders are about 6 feet apart, measured
across the track. The fire-box inside is 5 feet
long and 2 ft. 11 in. wide, and the cylindrical part of
the boiler is 4 feet in diameter measured on the outside
of the smallest portion. The water spaces around
the fire-box are about 3 inches wide. There are 140
tubes, which are 2 in. in diameter measured on their
outside, and 11 ft. long. The inside of the smoke-stack
is 16 in. in diameter, and it is 14 ft. 3 in. high
measured from the top of the rails. The tender carries
about 1,800 gallons of water and about 8,000 lbs.
of coal. When loaded it weighs about 40,000 lbs.,
making the total weight of the engine and tender
100,000 lbs.
The following is a list of parts designated by the
letters of reference on plates I, II,
III and fig. 40.
A, A, Cylinders. B, Main driving-axle. C C, Main connecting-rods. D D, Main crank-pins. E, E, Truck-wheels. F, Axle of trailing-wheels. G, Fire-box. H, H, H, Frames. I, I, Frame-clamps. J, J, Eccentrics. K, K, Rockers. L L, Links. M, Lifting-shaft. N, N, Lifting arms. O O, Reverse-lever. P P, Cylinder part of boiler. Q, Smoke-box. R R, Smoke stack or chimney. S, Pilot or cow-catcher. T, Head-light. U, Bell. V, Sand-box. W, Whistle. X, Dome. Y Y, Cab or house. Z, Back or trailing-wheel crank-pin. A′, Pump air-chamber. B′, B′, Main driving-wheels. C′ C′ C′, Supply-pipe. D′, Front platform. E′, Bumper timber. F′ F′, Back driving-wheels. G′, Coupling-pin. H′, Friction-plate. I′, Check-valve. K′ K′, Foot-board. L′, Lazy cock. M′, Mud drum. N′ N′, Driving springs. P′, Pump. R′, Drop-door or grate. S′, Steam gauge. T′ T′, Feed pipe. U′ U′, Forward eccentric rods. V′ V′, Backward eccentric rods. X′, Lifting-shaft spring. Y′ Y′, Dampers. Z′, Pushing-bar. a a′, Tubes. b b, Grate. c, Fire-box door. d d, Ash pan. f f, Exhaust-nozzles or blast-pipes. g, Safety-valve lever. h h, Cross-heads. i i, Running-board. j, Throttle-stem. l, Throttle-pipe. m m, Dry pipe. n, T-pipe. o o, Steam-pipe. p, Petticoat pipe. q, Smoke-box door. r, Piston. s, Spark-deflector or cone. t t, Wire-netting in stack. u u u, Boiler-lagging. v v, Truck-spring. w w, Sector or quadrant. x, Blow-off cock. e k, Reversing-rod. y, Truck centre-pin. z, Throttle-lever. a′ a, Tubes. b′ b′, Truck frame. c′ c′, Bed-plate. d′, Boiler brace. e′ e′, Sand pipe. f′ f′, Equalizing lever for driving wheels. g′ g′, Guide-bars or rods. h′ h′, Receptacle for sparks. i′ i′, Bell rope. j′ j′, Guide yoke. k′, Valve-stem. l′ l′, Truck equalizing lever. m′ m′ m′, Hand-rail. n′, Blow-off cock in mud drum. o′, Spring balance. p′, Pump plunger. q′ q′, Foot steps. r′, Brace to smoke-box and frame. s′ s′, Steam-chests. t′ t′ t′, Crown-bars. u′, Head-light lamp. v′, Main valve. w′, Blow-off cock handle. x′, Bell-crank for throttle-valve. y′, Piston-rod. z′, Draw-bar.
PART VII. THE LOCOMOTIVE BOILER.
Question 82.How does the quantity of steam generated
in locomotive boilers in a given time compare with that
generated in the boilers of stationary and marine engines?
Answer. Locomotive engine boilers must produce
much more steam in a given time, in proportion to
their size, than is required of the boilers of any other
class of engines, (excepting perhaps those of steam
fire-engines,) because the space which locomotive boilers
can occupy and also their weight is limited.
Question 83.How is their steam-generating capacity
increased above that of marine and stationary boilers?
Answer. By creating a very strong draft of air
through the fire and then passing the smoke and
heated air through a great many small tubes, which
are surrounded by water. By this means the smoke
and hot air are divided into many small streams or
currents which are exposed to the inside surface of
the tubes to which and to the surrounding water their
heat is imparted.
Question 84.How is the action of the exhaust steam
in producing a draft in the chimney explained?
Answer. The exhaust steam escapes from the cylinders
through one or two contracted openings or
exhaust-nozzles (f, Plate II, also shown in
fig. 40[21]),
which point directly up the centre of the chimney or
smoke-stack. The exhaust steam escapes from this
orifice with great velocity, and expands as it rises, so
that it fills the pipe p and the smoke-stack R R. It
thus acts somewhat like a plunger or piston forced
violently up the chimney, and pushes up the air above
it, and, owing to the friction of the particles of air,
carries that which surrounds it along up the stack,
from which it all escapes finally into the open air,
thus leaving a partial vacuum behind in the smoke-box.
The external pressure of the atmosphere then
forces in air through any and every opening in the
smoke-box, to take the place of that already drawn out
or exhausted from it. As the only inlet is through
the tubes, to which the gases of combustion have free
access from the fire-box, and as the external air can
only pass through the fire-grate, and through the
burning fuel, to reach the fire-box, there is a constant
draft of air through the grate as long as the waste
steam escapes from the blast-pipe and up the chimney.
It is thus that, within certain limits, the more
the steam that is required, the more the steam that is
produced; for all the steam used in the engine draws
in the air in its final escape, to excite the fire to generate
more steam.[22] Sometimes one blast-orifice is
used for each cylinder, as shown in plates II and III
and fig. 40; in other cases the exhaust steam from
each cylinder escapes through the same orifice.
[21] The term blast-orifice is also often used to designate these parts
of locomotives.
Question 85.How much water is it necessary to
evaporate in order to furnish the steam required to run an
ordinary train at its usual speed?
Answer. For an ordinary “American” locomotive,[23]
weighing 60,000 lbs. and with cylinders of 16 inches
diameter and 24 inches stroke, from 6,000 to 12,000
lbs. of water must be evaporated per hour.
[23] In speaking of “American” locomotives, we mean locomotives
like that shown in Plate I, with four driving-wheels and a four-wheeled
truck, and shall so use the term hereafter.
Question 86.How much water will a pound of coal
evaporate in ordinary practice?
Answer. The quantity of water which is converted
into steam by a pound of coal varies very materially
with the quality of the coal, and the construction and
condition of the boiler; but from 6 to 8 lbs. of water
per pound of coal is about the average performance of
ordinary locomotives. It is, therefore, necessary to
burn from 500 to 2,000 lbs. of coal per hour in order to
generate the quantity of steam required by ordinary
engines.
Question 87.How large a grate is needed to burn
this quantity of coal?
Answer. The maximum rate of combustion may be
taken at about 125 lbs. of coal on each square foot of
grate surface per hour, so that to burn 2,000 lbs. we
need a grate with about 16 square feet of surface.
Question 88.How much heating surface is needed
for a given size of grate?
Answer. In common practice about 50 square feet of
heating surface are given for each square foot of grate.
There are, however, no reasons for the proportions of
either grate or heating surface which are given, excepting
that it has been found that they work well
in practice. It is, however, quite certain that the
larger a boiler is, and the greater its heating surface
in proportion to the steam it must generate, other
things being equal, the more economical will it be in
its consumption of fuel, or, in other words, the more
water will it evaporate per pound of coal.
Question 89. Why is it necessary to use small tubes
or flues in order to have the required amount of heating
surface?
Answer. Because there is a great deal more surface
in a small tube of a given length, in proportion to the
space it occupies, than in a large one. Thus a tube
two inches in diameter and eleven feet long has 829
square inches of surface, and one four inches in diameter
has 1,658 square inches, or just double the quantity.
But the four-inch tube occupies four times as
much space as the other, as it is twice as high and
twice as wide. Therefore, in proportion to the space
it occupies, the tube which is two inches in diameter
has twice as much surface as the larger one. If we
compare a two-inch with an eight-inch tube, we will
find that the former has four times as much surface,
in proportion to its size, as the eight-inch tube. As
the size and weight of locomotive boilers are limited,
it is therefore necessary, in order to get the requisite
heating surface in the space to which we are confined,
to use tubes of small diameter.
Small tubes also have the advantage that they may
be made of thinner material, and yet have the same
strength to resist a bursting pressure from within, or a
collapsing pressure from without, as larger tubes made
of thicker metal. The advantage of thin tubes is,
that the heat inside of them is conducted to the water
outside more rapidly than it would be through thicker
metal, which is important when combustion is as
rapid as it is in locomotive boilers.
The reason tubes of smaller diameter than two
inches are not ordinarily used is because they are then
liable to become stopped up with cinders and pieces
of unconsumed fuel.
Question 90.How is the fire-box of a locomotive
constructed?
Answer. It usually consists of a rectangular box
(G, figs. 41 and 42) about
three feet wide[24] and, for
the size of engine we have selected as an example,
about five or five and a half feet long inside. This
box is composed of metal plates, either iron, steel or
copper, which, excepting on the front side, are from
⁵⁄₁₆ to ³⁄₈ of an inch thick. This box is called the
inside shell of the fire-box, and is surrounded by another
shell, A B C D E F, fig. 42, of either iron or
steel plates, of about the same thickness as those composing
the inside. This is called the outside shell
of the fire-box and, as already explained, is so much
larger than the inside that there is a space, called
the water-space, from 2¹⁄₂ to 4¹⁄₂ inches wide, on all the
sides of the fire-box between the inner and outer
plates.
[24] The width is dependent upon the distance between the rails, or
gauge of the road, as it is called. The above size is for a 4 feet 8¹⁄₂ in.
gauge.
The top g, g, of the inside shell, which is called the
crown-sheet or crown-plate, is flat, whereas the outside
shell is arched, as shown in fig. 42. To the front plate of
the inside shell the tubes a a′, a a′ are attached. For
this reason its thickness is usually made greater than
that of the other plates, and is usually from ³⁄₈ to ³⁄₄ of
an inch. The edges of one of the plates at each corner
of the fire-box, where they are united together, as
shown in figs. 41 and 42,
are bent at right angles, and
the other is fastened to it with rivets from ⁵⁄₈ to ³⁄₄ of
an inch in diameter.
The inside and the outside shells of the fire-box are
united to each other by a wrought-iron bar or ring
(A F, figs. 41 and 42) which completely surrounds
the inner shell and closes the water-space between
the two shells. This bar is bent and welded to the
proper form to extend around the bottom of the inside
fire-box, and it is riveted to both shells. The water
in the water-space is in free communication with the
rest of the water in the boiler; and thus the flat sides
of the respective shells of the fire-box are exposed to the
full pressure of the steam, which tends to burst the
outside shell and collapse the inside one. These flat
sides, by themselves, would be unable to resist the
strain upon them, but as the strain upon the respective
fire-boxes is in opposite directions, and necessarily
equal for equal areas of surface, tie-bolts, n, n,
n, n, (figs. 41 and 42,) or, as they are called stay-bolts,
which are from ³⁄₄ to 1 inch in diameter, are screwed
through the plates at frequent intervals, usually from
3¹⁄₂ to 4¹⁄₂ in. apart, so as to connect the two fire-boxes
securely together, the ends of the stay-bolts being also
riveted or spread out by hammering so as still further
to increase their holding power. These bolts, owing
to the expansion and contraction of the boiler and
other strains to which they are subjected, very frequently
break, and if they are made of solid bars of
metal there is no way of discovering with certainty
whether they are in good condition or not without
taking the boiler to pieces. They should therefore be
made of the best quality of wrought iron, brass or
copper and should also be made tubular, that is they
should have a hole through the centre, so that when
they break the water will escape at the fracture into
the hole and the leak will thus indicate the defect and
danger. The latter is much greater from this cause than
is usually supposed, and it is not unusual to find on
taking a boiler to pieces that a large number of the
stay-bolts are broken.
Fig. 41.
Scale ¹⁄₄ in. = 1 foot.
Fig. 42.
Scale ¹⁄₄ in. = 1 foot.
Question 91.How can the strain on the flat surface
of a boiler between the stay-bolts be calculated?
Answer. By MULTIPLYING THE AREA IN INCHES
BETWEEN ADJACENT STAY-BOLTS BY THE PRESSURE.
The reason for this is, that each stay-bolt must sustain
the pressure on a part of the plate to which it is
attached. Thus in fig. 43 it is plain that the bolt s
must sustain the pressure on one-half of that part of
the plate between it and the bolts v, t, w, u, around it,
or the pressure on the square a b d c, whose sides are
equal to the distance (4 inches) between the centres of
the bolts. With a pressure of 100 pounds per square
inch, the calculation would therefore be: 4 × 4 × 100 =
1,600 lbs. on each bolt.
Fig. 43. Scale 1¹⁄₂ in. = 1 foot.
Stay-bolts should never be subjected to a strain of
more than one-eighth or one-tenth of their breaking
strength.
Question 92.How do stay-bolts often fail without
breaking?
Answer. By tearing or stripping the thread of the
bolt, or that in the plate, but oftener perhaps by the
stretching of the plates between the holes. With a
heavy pressure, the tendency of the plates between
the holes, especially if they are heated very hot, is to
“bulge” outward and thus stretch the hole in every
direction until it is so large that the bolt is drawn out
without much injury to the screw-thread.
Question 93.How is the flat-top or crown-sheet
strengthened?
Answer. It is sometimes strengthened with stay-bolts
similar to those used for the sides, which pass
through the inner and outer shells;[25] but usually the
crown-sheet is strengthened by a series of iron bars,
(f, f, fig. 41 and 42) called crown-bars, placed on edge,
and of considerable depth, which are firmly fastened
to it by T-head rivets or bolts. The crown-sheet can
therefore only be crushed downwards by bending these
bars, which are of great strength. They usually extend
crosswise of the length of the fire-box, but are
sometimes placed lengthwise. These bars bear on the
fire-box only at each end, as shown in fig. 42, and are
usually made with a projection, k, k, which rests on
the edge of the side plates. Iron rings or washers
from ³⁄₄ to 1¹⁄₂ inches thick are interposed between the
plate and the bars at the points where the bolts or
rivets which secure the rivets pass through. This
permits the water to circulate under the bars, and prevents
the crown-sheet from being burnt or overheated,
as it would be if the water were excluded from the
whole under surface of the crown-bars. [26]The crown-bars
are also attached to the outer shell and the dome
by braces, e, e, l, l.
[25] This method of staying crown-sheets has been extensively used
on the Baltimore & Ohio and Reading railroads, and is now very generally
used in Europe.
The opening c, fig. 41, at the back end is for the
door through which fuel is supplied to the grate.
Question 94.How are the grates constructed?
Answer. They are generally made of cast-iron bars,
and for burning coal are usually arranged so that the
fire can be shaken by moving the bars. For burning
anthracite coal, the grates are sometimes made of
wrought-iron tubes, through which a current of water
circulates to prevent them from being overheated.
Question 95.How are cinders and burning coals
prevented from falling through the grate upon the road?
Answer. By attaching a sheet-iron receptacle or ash-pan
(d′ d′, fig. 41) as it is called, under the grate,
which it completely encloses from the outside air.
This then serves two purposes, as it is often important
when the engine is standing still to prevent any access
of air to the fire-box, and therefore the ash-pan
is made to fit tightly to the fire-box. Suitable doors,
or dampers as they are called, are placed in front and
behind, and sometimes on the sides, which can be
opened or closed to admit or exclude air as may be
needed.
Question 96.How are the tubes or flues of a locomotive
arranged?
Answer. They are fastened into accurately drilled
holes in the tube sheet (a, a, figs. 41 and 42) which
forms the front of the fire-box and in similar holes in
a plate (a′, a′, fig. 41,) which forms the front end of
the cylindrical part of the boiler. They thus connect
the fire-box with the smoke-box. The tubes are arranged
so that each tube will have a space of from ⁵⁄₈
to ⁷⁄₈ of an inch between it and those adjoining.
The position of the holes for the tubes in relation to
each other is determined by describing from the centre
of one tube (o, fig. 44) a circle with a radius, o k,
equal to the sum of the diameter of a tube and the
distance which they are intended to be apart, and then
subdividing this circle with the radius into six parts,
k, r, s, l, g and p. Each point of subdivision and also
the centre, o, of the circle will be the centre of a tube.
By drawing them from these centres it will be found
that the distances a b, c d between adjoining tubes
will be the same between all of them. By describing
circles from the centres of the outside tubes and subdividing
the circles as before the position of other tubes
will be determined around those first laid down. This
can, of course, be carried out indefinitely. A difference
in the arrangement of the tubes will be observed
if, when we subdivide the first circle shown in fig. 44,
instead of commencing from the intersection of a vertical
line we begin from a horizontal line, h i, as
shown in fig. 45. In the former case the tubes are
said to be in vertical rows, and in the latter in horizontal
rows. It is apparent from the figures and as shown
by the arrows that the water can circulate in ascending
currents more freely when tubes are arranged in
vertical rows than when they are arranged horizontally.
Fig. 44. Scale ¹⁄₄.
Fig. 45. Scale ¹⁄₄.
Question 97.How are the tubes fastened and made
water-tight in the tube-sheets?
Fig. 46. Scale ¹⁄₄.
Fig. 47.
Answer. They are inserted into the holes drilled to
receive them, and the ends are allowed to project about
a quarter of an inch beyond the tube-sheets. A tapered
plug, fig. 46, is then driven into the tube, to expand
it so that it will fit the hole. A tool is used
called a tube-expander, fig. 47, which is what might be
called an expanding plug, consisting of a number of
sections, a, b, c, d, e, f, g, h, held together by a spring
clasp s, which embraces them, as shown in the engraving.
This plug when the sections are drawn together
is inserted into the mouth of the tube, and the
tapered plug p p, is then driven into the opening left
in the center of the cluster of sections, which are thus
expanded. By this means, the ridge a b c d expands
the tube at the inner edge of the tube-sheet,
forming a ridge or corrugation, as shown at c c, fig.
48. At the same time the shoulder j k l on the tool
expands the outer edge of the tube somewhat as is
shown at f f, fig. 48. By repeating this process, and
slightly turning the expander each time, the tubes can
be made perfectly water-tight. There are other forms
of tube-expanders, but the one described, known as
Prosser’s expander, is more generally used than any
other. In many cases, after the tubes are expanded
with the tool described, the outer edge is turned over
still more with what is called a thumb-tool, fig. 49,
probably from its resemblance in form to a man’s
thumb. By placing the curved shoulder a on the end
f, fig. 48, of the tube it is turned over, somewhat in
the form shown in the engraving, by repeated blows of
a hammer on the end of the tool. Copper ferrules,
represented by the black shading, a a, are also much
used now on the outside of locomotive tubes, and it is
said that with them the joints can be kept tight much
easier than without. By turning over the outside
edge of the tube as shown in fig. 48, it not only protects
the copper ferrule, but, as the tubes must act as
braces to sustain the pressure of steam in the flat
tube-sheets, it gives the joints the requisite strength
for resisting such strains.
Fig. 48. Scale ¹⁄₄.
Fig. 49.
Question 98.How can the strain on the cylindrical
part of a boiler be calculated?
Answer.By multiplying the diameter in
inches by the length in inches and the product
by the steam-pressure per square inch.
Thus for a boiler 48 inches in diameter and 10 feet
long with 100 pounds pressure the calculation would
be 48 × 120 × 100 = 576,000 lbs.
Question 99.Why do we multiply the diameter, instead
of the circumference, by the length, to get the strain
on the cylindrical part?
Answer. The reason for multiplying by the diameter
instead of by the circumference is because only a portion
of the pressure on the inside surface of the boiler
exerts a force to burst the shell at any one point.
Thus, supposing the following diagram, fig. 50, to
represent a section of a boiler, if we have a force acting
on the shell in the direction of the line a b, at the
point b, where it is exerted against the shell of the
boiler, it would be composed of two forces, one acting
in the direction b e, and tending to tear the boiler
apart on the line c d, and the other acting in the direction
f b, to tear it apart on the line h g. It is so
with all pressure inside the boiler, excepting that, say
a h, which acts exactly at right angles to the line of
rupture c d, it is all composed of two forces, only one
of which tends to tear the boiler apart at one point.
It is therefore only a part of the pressure on the circumference
which tends to burst the boiler at a given
place, and that part is equivalent to the pressure on
a surface whose width is equal to the diameter and
not the circumference.
Fig. 50.
Fig. 51.
This we know is a little difficult for those to understand
who are not familiar with the principles of what
is called the “resolution of forces,” and we will therefore
try to make it clear in another way.
To do this we will suppose that we have a boiler,
a b, fig. 51, made in two halves and bolted together
at a and b by flanges. It is evident that if we brought
a pressure against the inside of the flanges in the direction
of the darts c and d, such a pressure would
not have a tendency to tear apart the bolts a and b.
Some distortion of the boiler might in fact take place,
if, for example, we put a jack-screw inside and forced
out the flanges as indicated, without subjecting the
bolts to a tensile strain. We see therefore that the
forces acting in the direction c and d have no tendency
to tear apart the bolts at a and b, but it is only
the forces such as e, f and g, which act at right angles
to a b, that exert a strain on the flanges.
That this force is equivalent to a pressure on a surface
with a width equal to the diameter of the boiler
is apparent if we suppose that we have a boiler, a b,
fig. 52, and that each half, c and d, is nearly filled
with some substance, say wood or cement, which is
fitted so tight that no steam can get between it and
the shell of the boiler. It is apparent now that if we
admit steam into the space f, the force exerted on the
bolts a and b is that due to the pressure on the surface
of the wood or cement exposed to the steam whose
width is equal to the diameter of the boiler. It might
be said though that if this substance were elastic, like
india-rubber, the effect of the steam would be different.
If it were elastic, and a pressure on the surfaces f
caused it to spread in the direction g and h so as to
produce a pressure in those directions, it would, as has
already been shown, not exert a force on the bolts a
and b to tear them apart, but have a tendency to rupture
the boiler at right angles to a b. The sides of
the boiler must therefore have a strength sufficient to
resist this force which tends to tear them asunder. If
the boiler is made of iron ³⁄₈ inch thick there would be
a sectional area of 45 square inches on each side, or a
total of 90 square inches, to resist this strain, so that
each square inch must bear 6,400 lbs. of strain. The
correctness of this rule can be demonstrated by the
use of mathematics, which would be out of place
here. Its practical truth has however been proved by
experiment.
Fig. 52.
Question 100.How much strain per square inch is
good boiler plate capable of resisting, and how much is it
safe to subject it to?
Answer. There is great variation in the tensile
strength[27] of rolled iron boiler plate, but that of good
plate will average about 50,000 pounds per square inch,
if the strain is applied in the direction of the “grain”
or the fibres of the iron[28], and about ten per cent. less
if the strain is applied crosswise of the grain. It has,
however, been found by experiment that when a tensile
strain is applied to a bar of iron or other material,
it is stretched a certain amount in proportion to the
length of the bar and to the degree of strain to which
it is subjected. It is found that if this strain does not
exceed about one-fifth of that which would break the
bar, it will recover its original length, or will contract
after being stretched, when the strain is removed.
The greatest strain which any material will bear
without being permanently stretched is called its
limit of elasticity, and so long as this is not exceeded
no appreciable permanent elongation or “set” will be
given to iron by any number of applications of such
strains or loads. If, however, the limit of elasticity is
exceeded, the metal will be permanently elongated,
and this elongation will be increased by repeated applications
of the strain until finally the bar will break.
At the same time the character of the metal will be altered
by the repeated application of strains greater
than its elastic limit, and it will become brittle and less
able to resist a sudden strain, and will ultimately break
short off. It is therefore unsafe to subject iron, or in
fact any other material, to strains greater than its
elastic limit. This limit for iron boiler plates may be
taken at about one-fifth its breaking, or, as it is called,
ultimate strength. It should be remembered, however,
in this connection, that it often happens that the
steam pressure is not the greatest force the boiler
must withstand, as sudden or unequal expansion and
contraction are probably more destructive, to locomotive
boilers especially, than the pressure of the steam.
[27] A force exerted to pull any material apart is called a tensile strain,
and if exerted to compress it is called a compressive strain.
[28] It should be explained that in the process of manufacturing iron
by rolling, the iron is stretched out into fibres in the direction in which
it passes between the rolls.
Question 101.How are the plates of boilers fastened
together?
Answer. With rivets, which are made with a head
at one end, and are inserted while they are red-hot
into holes drilled or punched in the edges of the
plates. After they are in the holes a head is
formed on the other end, either with blows from hand
hammers, or by a machine constructed for the purpose.
In these machines the rivet after it is in the
holes is brought between a fixed and a movable die, the
head which is made with the rivet being placed against
the fixed die, and the movable die is then pressed,
either by steam or hydraulic pressure with great force
against the other end of the rivet, thus forcing the end
of the rivet into the form of the die, which is made of
the proper shape and size for the rivet head. The
powerful pressure which is thus brought on the rivet
causes it to be pressed into all parts of the two holes,
thus completely filling them both; whereas with hand
riveting, the holes are not nearly so completely filled,
as it is impossible with blows of a hammer to subject
the rivets to so powerful or uniform a pressure as
the machine brings upon them.
Fig. 53.
Question 102.What is the strength of riveted seams
compared with that of the solid plate?
Answer. The strength of a riveted seam depends
very much upon the arrangement and proportion of
the rivets, but with the best design and construction,
the seams are always weaker than the solid plates, as
it is always necessary to cut away a part of the plate
for the rivet holes, which weakens the plate in three
ways: 1. By lessening the amount of material to resist
the strains. 2. By weakening that left between
the holes. 3. By disturbing the uniformity of the distribution
of the strains. The first cause of weakness
is obvious from an inspection of an ordinary seam,
riveted with a single row of rivets, fig. 53. In this
we have two plates 7¹⁄₂ inches wide and ³⁄₈ thick fastened
with four rivets ¹¹⁄₁₆ inches in diameter and 1⁷⁄₈
inches from centre to centre. The section of the
plate calculated with decimals[29] would therefore be
.375 × 7.5 = 2.81 square inches. A piece ¹¹⁄₁₆ inch wide
and ³⁄₈ inch thick would be removed to form each
hole, or a sectional area for the whole plate of .375 ×
.6875 × 4 = 1.03 square inches, so that the section of
the plate would be reduced through the holes 2.81 -
1.03 = 1.78 square inches. In other words, on the dotted
line a b it will have only about 63 per cent. of
the sectional area of the solid plate.
[29] In the following calculations all the dimensions have for convenience
been reduced to decimals.
The second cause of the reduction of strength is
owing to the injury sustained by the plates during the
process of drilling and punching. The knowledge existing
regarding this subject is not very accurate, although
numerous experiments have been made to determine the
exact amount of weakening caused by punching plates.
It is, however, certain that in many cases the strength
of the metal left between the holes of boiler plates is
reduced from 10 to 30 per cent. by the process of
punching. It is probable, however, that soft ductile
metal is injured less than that which is harder and
more brittle. Some kinds of steel plates are especially
liable to injury from punching. It is also probable
that the condition of the punch, and the proportions
of the die used with it, have much to do with its effect
upon the metal
The third cause of weakness is owing to the fact
that if one or more holes are made in a plate of any
material, and it is then subjected to a tensile strain,
the strain, instead of being equally distributed through
the section left between the holes, will be greatest in
that part of the metal nearest them. This can be illustrated
by taking a band of india-rubber, fig. 54, and cutting
a round hole in it to represent a rivet hole. If we
draw two parallel lines, A B, across the band and then
stretch it, the lines, instead of remaining parallel
when the band is stretched, will separate most next
to the hole, as shown in fig. 55, indicating that the
fibres of the rubber nearest the hole are strained most.
A similar effect takes place when a plate of iron is
stretched, so that a fracture is liable to begin next to
the hole, after which the plate will be broken as it
were in detail.
Fig. 54.
Fig. 55.
Question 103.How may a boiler seam like that
shown in fig. 53 break?
Answer. It may break in three different ways:
1. By the plate tearing between the rivet holes on
the line a b.
2. By the rivets shearing off.
3. By the plate in front of the rivets crushing, as
shown in fig. 56.
Fig. 56.
Question 104.How can the strength of a boiler
seam be calculated at each of these three points?
Answer. The strength through the rivet holes is
calculated by TAKING THE AREA IN SQUARE INCHES
OF THE METAL WHICH IS LEFT BETWEEN THE RIVET
HOLES, AND MULTIPLYING IT BY THE ULTIMATE
STRENGTH OF THE METAL AFTER THE HOLES ARE
MADE. Thus, in fig. 53, the area of each of the plates
between the rivet holes is 1.78 square inches. As already
stated, good boiler plate will break at a strain
of about 50,000 pounds in the direction of its fibres,[30]
but the strength of the metal left between punched
holes is probably 20 per cent. and that between
drilled holes 10 per cent. less than that of the solid
plate. We must, therefore, in calculating the strength
of a punched seam, take the ultimate strength of the
metal between the holes at only 40,000 pounds per
square inch. The calculation for the strength through
the holes would therefore be: 1.78 × 40,000 = 71,200
pounds.
[30] Boiler plates should always be so arranged that the greatest strain
will come on them in the direction of their greatest strength, which is
parallel with the fibres of the metal.
It has also been found by experiment that the
strength of rivets to resist shearing is about the same
as that of good boiler plate to resist tearing apart, or
50,000 lbs. per square inch. The strength of the rivets,
therefore, is calculated by MULTIPLYING THE AREA
IN SQUARE INCHES OF ONE RIVET BY THE NUMBER
OF RIVETS, AND THE PRODUCT BY THE STRENGTH
OF THE METAL TO RESIST SHEARING. The calculation
for fig. 53 would therefore be:
Area of ¹¹⁄₁₆ rivet = .3712 × 4 × 50,000 = 74,240.
or a little more than the strength of the plates through
the holes.
The resistance offered by a plate to the crushing
strain of a rivet has been found also by experiment to
be about 90,000 pounds per square inch. It can be
proved that the area which resists the crushing strain
of a rivet in a plate, fig. 53, IS MEASURED BY MULTIPLYING
THE DIAMETER OF THE RIVET BY THE
THICKNESS OF THE PLATE. The calculation for the
strength of this part of the seam will therefore be: diameter
of hole = .6875 × .375 × 4 × 90,000 = 92,812.
The strength of the solid plate would be EQUAL TO
ITS SECTIONAL AREA MULTIPLIED BY 50,000 POUNDS,
or 7.5 × .375 × 50,000 = 140,625 pounds. The ultimate
strength of our seam would then be as follows:
Plates through rivet holes
(tearing)
=
71,200
lbs.
Rivets
(shearing)
=
72,240
lbs.
Plates in front of rivets
(crushing)
=
92,812
lbs.
Solid plate
(tearing)
=
140,625
lbs.
It will thus be seen that the strength of the weakest
part of the above seam, fastened with a single row of
rivets in punched holes, is very little more than half
(50.6 per cent.) of that of the plates. It will be noticed
that the weakest part of the seam is the plates
between the holes.
Fig. 57.
Fig. 58.
Fig. 59.
Fig. 60.
Question 105.How can the strength of such a single-riveted
boiler seam be increased?
Answer. The most obvious way of increasing the
strength of such a seam is to place, or, as it is called,
space, the rivets further apart, which would leave more
metal between the holes, and thus strengthen the seam
at its weakest part. But if this is done, it is said that
there is difficulty in keeping the seam water-tight, as
the plates are then liable to spring apart between the
rivets. Another way of increasing its strength is to
drill the rivet holes. As already stated, the difference
in the strength of the metal left between drilled and
punched holes has been shown to be from 10 to 20 per
cent. There is also another advantage in drilling the
holes for rivets. In punching them, it is necessary to
punch each plate separately, and even with the utmost
care and skill it is impossible to get the holes to match
perfectly. Some of them will overlap each other, as
shown in fig. 57, so that when the rivet is set, it will
assume somewhat the form shown in fig. 58. There
is then danger that those rivets which fill the holes that
match each other will be subjected to an undue strain.
If, for example, we have five rivet holes, as shown in
fig. 59, and only the centre ones correspond with each
other, then the rivets in all the other holes will assume
somewhat the form shown in fig. 58, and therefore
the centre rivet c, in fig. 59, which fits the holes
accurately, must take the strain of the other four until
they draw up “to a bearing.” Under such circumstances,
which are not unusual, there will be great
danger either of shearing off the rivet c, or of starting
a fracture in the plates, as indicated by the irregular
line a b, between the adjoining rivets. It is also obvious
that a rivet like the one in fig. 58 will not hold
the plates together so well as one which fits more perfectly,
as shown in section in fig. 53, and therefore
there is more danger of leakage between the plates
from badly fitted rivets than from those which fill
the holes more perfectly; consequently rivets which
fit imperfectly must be placed nearer together than
those which are well fitted. It is true that rivets
which are set with a riveting machine fill any inaccuracies
of the holes more perfectly than those which are
set by hand. But even if they are made to fill the
holes as shown in fig. 60 they are still not so strong
to resist shearing nor so efficient in holding the
plates together as they would be if the holes conformed
more perfectly to each other. In drilling the holes,
the second plate can be drilled from the holes in the
first, so that the holes in each will correspond with
each other perfectly. The rivets will therefore fit
more accurately, and consequently can be spaced further
apart, and still keep the plates tight, and thus
have more material between the holes, which is the
weakest part of the seam. It has been shown that a
rivet ¹¹⁄₁₆ inch in diameter has a resistance to shearing
of 18,560 pounds. There is therefore no advantage
in spacing such rivets further apart than 1¹³⁄₁₆
from centre to centre, because the metal left between
drilled holes that distance apart would be slightly
stronger than the rivets. If therefore the rivets are
placed further apart, their diameter must be increased.
There is, however, a limit beyond which the diameters
of rivets cannot be increased with advantage, because
if we increase their diameters, their sectional area to
resist shearing is increased in proportion to the square
of the diameter, whereas the section of metal in the
plate to resist crushing is increased only in proportion
to the diameter. This will be apparent if we compare a
rivet ¹⁄₂ inch with one 1 inch in diameter. The first has
a sectional area of .1963 inch, the other .7854 inch, or
four times that of the first one. Now the area which resists
the crushing strain of the rivets is increased only in
proportion to their diameters, or is twice as much for
the one as for the other. If, therefore, we increase
the diameters of the rivets, we very soon reach a
point at which the plate has less strength to resist
crushing than the rivet has to resist shearing. The
diameter of rivet which will give just the same resistance
to both strains varies with the thickness of the
plates; with ³⁄₈ inch plates a ⁷⁄₈ rivet will have a resistance
to shearing of 30,065 pounds and the plate in
front of it a resistance to crushing of 29,530 pounds.
A ⁷⁄₈ rivet is, therefore, the largest size which can be
used to advantage in ³⁄₈ plates. If now we were to
space such rivets so far apart that the metal left between
the holes would have a strength just equal to
that of the rivets, we would have the strongest possible
seam that can be made with a single row of rivets.
This distance would be 1³⁄₄ inches between the edges
of the rivets, or 2⁵⁄₈ from center to center, as shown in
fig. 61. The following table will show the strength of
such a seam composed of four rivets, and two plates
10¹⁄₂ inches wide,[31] with drilled holes:
Plates through rivet holes
(tearing)
118,125
lbs.
Rivets
(shearing)
120,260
lbs.
Plates in front of rivets
(crushing)
118,125
lbs.
Solid plates
(tearing)
196,875
lbs.
[31] It has been necessary to take for an illustration, plates of a different
width from the preceding example, in order to get an even number of
spaces between the rivets in each case.
Fig. 61.
From this it is seen that the strength of the seam
with drilled plates is 60 per cent. of that of the solid
plates, or it is about 18¹⁄₂ per cent. stronger than that
made with plates having punched holes and the rivets
nearer together. It should be noted that a great part
of the superiority of the seams made with drilled holes
is due to the superior accuracy of the work done in
that way, which makes it possible to use larger rivets
spaced further apart. It is probable that with the use
of some recently designed machines, intended to produce
greater accuracy in punching rivet holes, part of
the above advantage may be realized with that kind of
work. The greatest distance that rivets may be
spaced apart without incurring danger of leakage between
the plates must, however, be determined more
by practical than theoretical considerations. It is certain,
however, that rivets may be spaced much further
apart than they are in ordinary practice, and the
seams still be kept tight, if the work is done with sufficient
accuracy and care.
Question 106.What other methods are there of
making boiler seams which are stronger than those which
have been described?
Answer. In this country two rows of rivets are used
and also what is called a “welt,” or covering-strip,
the latter with both single and double-riveted seams.
Fig. 62.
Question 107.How are the rivets arranged when
two rows are used?
Answer. They are often placed just behind each
other as shown in fig. 62, which is called chain-riveting.
Such an arrangement of rivets obviously adds nothing
to the strength of the seam, because its weakest part,
as has already been shown, is the section of the plates
through the rivet-holes, and this is not at all strengthened
by adding another row of rivets, because the
plates are just as liable to break through the rivet-holes
with two rows of rivets as they would be with
one.
Fig. 63.
A much better arrangement is to place them alternately
in the two rows, as shown in fig. 63. Rivets
arranged in that way are said to be staggered, or placed
zigzag. The method of laying off the holes and proportioning
such a seam in order to get the most
strength is, first, to determine the greatest distance
which can be allowed between the rivet-holes, and yet
keep the seams water-tight. Supposing this is 1⁵⁄₁₆
inches,[32] with plates ³⁄₈ inch thick, the diameter of rivet
whose sectional area will give an equal amount of
strength must then be calculated. From the preceding
data it will be found that for drilled plates the
resistance of the portion left between such holes will
be 22,148 pounds, and a rivet ³⁄₄ inch in diameter will
have a resistance of 22,085 pounds. On the line a b,
fig. 63, which is to be the first row of rivets, we will
draw one hole, c. From the center of this hole we
will describe the arc of a circle, d e, with a radius, c d,
equal to the sum of the distance between the holes,
1³⁄₈ inches, and one-half the diameter of the hole, or ³⁄₈
inch, making the radius 1³⁄₄ inches. From d, the intersection
of this arc with the line of rivets, a b, with
the same radius, we will step off the distance d f will
then be the centre of the second rivet-hole on the line
a, b. The rivet can therefore be drawn, and from its
centre, with the same radius employed before, another
arc, d g, should be drawn. If now we draw a rivet-hole
(h) between the two arcs and touching each of
them, we will have all three of the holes so arranged
that the metal between the holes c, f, will be just
equal to that between them and the hole h. In other
words, the strength of the plates on the line c f is
just the same as on the line c h f. Therefore the
strength of the plates on the straight line a b is just
the same as on the zigzag line c h f, etc. The
strength of this seam would therefore be as follows:
Plates through rivet-holes
(tearing)
110,742
lbs.
Rivets
(shearing)
110,425
lbs.
Plates in front of rivets
(crushing)
126,562
lbs.
Solid plates
(tearing)
158,205
lbs.
[32] That and even greater distances between the edges of the holes are
now used successfully with ³⁄₈-inch plates.
The weakest portion of this seam, it will be seen,
has a strength of 70 per cent. of the plate, or is 38 per
cent. stronger than a single-riveted seam with punched
holes. If we were to use ⁷⁄₈ inch rivets and make the
spaces between them 1³⁄₄ inches, the strength of a similar
seam would be as follows:
Plates through rivet-holes
(tearing)
147,656
lbs.
Rivets
(shearing)
150,325
lbs.
Plates in front of rivets
(crushing)
147,656
lbs.
Solid plates
(tearing)
205,078
lbs.
This seam would then have a strength of 72
per cent. of the solid plates, or be 42¹⁄₄ per cent.
stronger than the ordinary riveted seam with punched
holes. It is important to observe that an increase of
strength results from the use of larger rivets spaced
farther apart than is usual in ordinary practice, and
that this is possible only with the best and most accurate
workmanship.
Fig. 64.
Question 108.What is the form of construction of
boiler seams made with a welt or covering-strip?
Answer. The plates (a, b, fig. 64) are lapped over
each other as for an ordinary seam. Another plate, c,
about nine inches wide, is then placed on the inside of
the seam and bent so as to conform to the lap of the
two plates. The rivets r, whether a double or single
row, pass through all three plates, and two more rows
of rivets are put next to the edges of the covering
plate, c. It is plain that the strength of the seam, r,
is increased up to a certain point by an amount just
equal to that of the rivets in the edges of the covering
plate. If, however, these are placed too close together,
the plates a and b will be weaker through the outside
rows of rivets than the seam is through either of the
outside ones and the middle one taken together. If,
for example, we take a single-riveted seam, like that
shown in fig. 53, whose strength is only a little more
than half that of the solid plate, and should add to it
a covering plate, as shown in fig. 64, and then space
the rivets in the edges of the covering plate the
same distance apart as in the middle seam, then obviously
the plates would be just as liable to break
through the outer rows of holes as through the center
row before the covering plate was added. If, however, the
holes in the two outside plates are spaced at say twice
the distance apart, or 3³⁄₄ inches, then the only way the
seam can break through the outer rows of holes is by
shearing the rivets, because the plates between the
holes are then stronger than the rivets. But before
these rivets can be sheared, the centre seam must give
way. Thus the strength of such a seam is equal to
THE SUM OF THE STRENGTH AT THE WEAKEST
POINTS OF THE MIDDLE AND THE OUTSIDE SEAMS.
The strength of the plates between the holes of the
outside rows of rivets must, however, be as great as
the sum referred to, otherwise the seam will be the
weakest at that point, and the failure will occur there.
The rivets in the outside rows should be spaced at least
twice as far apart as those in the middle seam. The
number of rivets to resist shearing will then be 50 per
cent. greater, so that the strength of a seam like that
shown in fig. 53, with a covering plate added, will be
as follows:
Plates through outside rows of rivet-holes
(tearing)
91,880
lbs.
Rivets in one outside and middle row
(shearing)
111,360
lbs.
Plates in front of rivets
(crushing)
139,218
lbs.
Solid plates
(tearing)
140,625
lbs.
An ordinary single-riveted seam with punched
holes, with a welt or covering plate added, would thus
have a strength equal to 65.3 per cent. of the solid
plate, or be 29 per cent. stronger than the seam without
the covering plate. It is probable, however, that
the injury to the plate from punching the outside rows
of holes which are further apart is not so great as it is
when they are punched nearer together and to the
edge, so that the strength is somewhat greater than
our estimate.
The relative strength of the different forms of seams
described in percentage of the strength of the solid
plate is then as follows:
Percentage of strength compared with solid plate.
Single-riveted seam, punched holes
¹¹⁄₁₆ rivets
50
.6
Single-riveted seam, drilled holes
⁷⁄₈ rivets
60
.
Double-riveted seam, drilled zigzag holes
³⁄₄ rivets
70
.
Double-riveted seam, drilled zigzag holes
⁷⁄₈ rivets
72
.
Single riveted seam, punched holes with covering plate
65
.3
Question 109.Are there any other forms of boiler
seams used?
Answer. In Europe what are called butt-joints are
used to some extent. In these the ends of the two
plates abut against each other, with a covering strip
on one or both sides. This form of joint is, however,
not used in this country, and therefore its peculiarities
will not be described.
Question 110.How are the seams of boilers made
water-tight?
Answer. By what is called caulking. That is, by the
use of a blunt instrument somewhat resembling a
chisel, the end of which is placed against one or both
of the edges of the plates c, d, fig. 53, which are then
riveted down by blows of a hammer, somewhat as the
joints of a ship are made tight. Before the edges,
which are called the caulking edges, of the plates are
made tight in this way, they are cut or trimmed off with
a chisel. In this process the plate under the edge is
often injured seriously by the carelessness of workmen,
who sometimes allow the chisel to cut a groove
in the plate under the edge, thus weakening it at a
point where the greatest strength is needed. There
is also danger of forcing the plates apart in the manner
shown in fig. 65, if it is done carelessly and with
a heavy hammer.
Fig. 65.
Question 111.How are the flat ends of the boiler
strengthened?
Answer. By braces, u, u, r, r, fig. 41, which are fastened
to the end plates and to the outer shell of the
boiler. They are fastened at one end to ⟂ shaped
pieces called crow-feet, which are riveted to the end
plates of the boiler. At the other end they are made
with a broad foot, which is riveted to the outer shell
of the boiler. Especial attention should be given to
the form, proportion and arrangement of these braces
when a boiler is constructed, and they should be frequently
examined while the engine is in use, as they
are liable to be neglected or carelessly constructed and
to become weakened or broken by corrosion, or
the constant strain to which they are subjected.
Great ignorance is often displayed in the design and
proportions of these braces, especially in their attachments
to the shell of the boiler.
Question 112.How should the braces for strengthening
the ends of a boiler be proportioned?
Answer. Every part should be made equally strong.
If, for example, the brace itself is made of a bar of round
iron one inch in diameter, its sectional area would be
.7854 square inch. The iron used for these braces
should be of such strength that a force of not less than
50,000 lbs. per square inch of transverse section should
be required to tear it apart lengthwise. A bar of the
size referred to would therefore require not less than
39,270 pounds to pull it apart. All the other parts
should be capable of resisting an equal strain. It is,
for example, not unusual to find a brace of the size we
have described, and even of larger diameter, fastened
to a crow-foot which is attached to the boiler plate with
two rivets ⁵⁄₈ inches in diameter. A similar fastening
for the other end of the brace is also often used. The
sectional area of these two rivets is considerably less
than that of the brace, and at the same time the strain
is brought upon them at such an angle as to have a
tendency to “snap” them off. For this reason, and
also because a rivet is apt to be deteriorated in
strength by the hammering, the rivets should always
have a sectional area very nearly or quite double that
of the bar which forms the brace. The metal around
the eyes through which the pins are inserted should also
be carefully proportioned, and the transverse section at
any one point should always be at least 1¹⁄₂ times greater
than that of the bar. The area of the pins used for
attaching the bars to the crow-feet should always be a
little more than half that of the bar. That is, an inch
bar should have a pin not less than ³⁄₄ inch in diameter.
When flat braces are used, it is not unusual to
find a bar 3 inches wide with a hole an inch in diameter
punched or drilled so near the end that a pin is
sure either to pull out the end of the bar or else to
break it crosswise at the hole with a much less strain
than the brace itself would resist. The ends of braces
should always be enlarged enough to give them sufficient
strength to resist as much strain as the bar itself.
Although these precautions may appear unimportant,
and unfortunately are often so regarded, yet it is
upon just such details as these that the lives and the
safety of every locomotive runner, fireman and others
near them are constantly dependent.
Question 113.How much water is usually carried in
a locomotive boiler?
Answer. There must always be enough water in the
boiler to cover completely all the parts which are exposed
to the fire, otherwise they will be heated to so
high a temperature as to be very much weakened or
permanently injured. In order to be sure that all the
heating-surface will at all times be covered with water,
it is usually carried so that its surface will be from 4
to 8 inches above the crown-sheet.
Question 114.How much space should there be over
the water for steam?
Answer. No exact rule can be given to determine
this. It may, however, generally be assumed that the
more steam space the better. In order to increase
the steam room, locomotive boilers are very generally
made in this country with what is called a wagon-top,
C, fig. 41, that is, the outside shell of the boiler
over the fire-box is elevated from 4 to 12 or even 18
inches above the cylindrical part.
Question 115.What is a steam-dome and for what
purpose is it intended?
Answer. A steam-dome, X, fig. 41, is a cylindrical
chamber made of boiler-plate and attached to the top
of the boiler. Its object is to increase the steam room
and to furnish a reservoir which is elevated considerably
above the surface of the water, from which the
supply of steam to be used in the cylinders can be
drawn. The reason for drawing the steam from a
point considerably above the water is that during
ebullition more or less spray or particles of water are
thrown up and mixed with the steam. When this is
the case, steam is said to be wet, and when there is
little or no unevaporated water mixed with it it is said
to be dry. It is found by experience that wet steam
is much less efficient than that which is dry. There is
also danger that the cylinders, pistons or other parts of
the machinery may be injured if much water is carried
over from the boiler with the steam, because
water will be discharged so slowly from the cylinders
that there is not time for it to escape before the
piston must complete its stroke, so that the cylinder-heads
will be “knocked out,” or the cylinder itself or
the piston will be broken. The reason for drawing or
“taking” steam from a point considerably above the
water is because there is less spray there than there
is near the surface, and the hottest steam, which is
also the dryest, ascends to the highest part of the
steam space.
Question 116.Where is the dome usually placed?
Answer. In this country it is usually placed over
the fire-box, but in Europe it is placed further forward,
either about the centre of the boiler or near the
front end of the tubes. Sometimes two domes are used
on engines, in this country, one over the fire-box and
another near the front end.
Question 117.How is the steam conducted from the
dome to the cylinders?
Answer. By a pipe I m m, fig. 41, called the dry-pipe,
which extends from the top of the dome to the
front tube-plate. On the front side of the tube-plate
and inside the smoke-box two curved pipes, O, fig. 41,
(shown also in fig. 40,) called steam-pipes, are attached
to the dry-pipe at one end, and to the cylinders at the
other. The vertical portion of the dry-pipe in the
dome, sometimes called the throttle-pipe, is usually
made of cast iron, the horizontal part of wrought iron,
and the steam pipes of cast iron.
Question 118.How is the loss of heat from locomotive
boilers by radiation and convection prevented?
Answer. By covering the boiler and dome with
wood, called lagging, about ⁷⁄₈ inch thick, which is a poor
conductor of heat, and then covering the outside of the
wood with Russia iron, the smooth, polished surface of
which is a poor radiator of heat.
Question 119.What is the smoke-box for?
Answer. The smoke-box Q is simply a convenient
receptacle for the smoke before it escapes into the
chimney or smoke-stack, which is attached to the top
of the smoke-box. It also affords a convenient place
for the steam and exhaust pipes, where they are surrounded
with hot air and smoke, and not exposed to
loss of heat by radiation. The front end of the smoke-box
is usually made of cast iron, with a large door in
the centre which affords access to the inside.
Question 120.How are the chimneys or smoke-stacks
of locomotives constructed?
Answer. The forms of smoke-stacks which have been
used are almost numberless. For burning bituminous
coal and wood they are generally made with a central
pipe, R, fig. 41, and a conical-shaped cast-iron plate,
S, called the cone or spark deflector, which, as the latter
name implies, is intended to deflect the motion of the
sparks and cinders which are carried up with the ascending
current of smoke and air in the pipe R, so as
to prevent them from escaping into the open air while
they are incandescent, or “alive.” A wire netting, t t,
is also provided, which is intended as a sort of sieve to
enclose the sparks and cinders, and at the same time
allow the smoke to escape. The receptacle h h is intended
as a chamber in which the burning cinders
will be extinguished before they escape. For burning
anthracite coal, a simple straight pipe, without a deflector
or wire netting, is ordinarily used.
Question 121.What are the proportions and materials
usually employed in the construction of smoke-stacks?
Answer. The inside pipe R, fig. 41, is usually made
of the same diameter as the cylinders, or an inch or
two smaller. For the other dimensions there are no
established rules, excepting for the height of the top
of the chimney above the rail, which is usually from
14 to 15 feet. The outsides of smoke-stacks are made
of sheet iron, but the upper part is now sometimes
made of cast iron, so as to withstand the abrasion of
the sparks and cinders longer than sheet iron will.
For very warm and damp climates, the outsides of
smoke-stacks are sometimes made of copper to resist
corrosion, which is very destructive to all iron structures
in those countries. The wire netting is made
of iron or steel wire from ¹⁄₁₀ to ¹⁄₃₀ of an inch in
diameter, and with from 3 to 4 meshes to the inch.
Question 122.What is the pipe N, fig. 41, intended
for?
Answer. It is intended to conduct the exhaust
steam and a portion of the smoke from the bottom of
the smoke-box, where the steam escapes, to the base
of the smoke-stack. In nearly all European engines,
the exhaust steam escapes at the top of the smoke-box
just below the aperture of the smoke-stack.
There is, however, often difficulty in equalizing the
draft in the tubes, that is, to get an equal amount of
smoke to pass through all of them. By the use of the
pipe P, called the inside pipe or petticoat pipe, it is
thought that the draft in the tubes can be equalized
much better, as a part of the smoke is drawn out of
the smoke-box at the top and part at the bottom of
the smoke-box. The pipe is usually made in two
parts, which slide into each other like a telescope.
The distance of the upper end from the top of the
smoke-box and that of the lower end from the bottom
can thus be increased or diminished, and if the draft is
greater through the upper tubes than through the
lower ones, or vice versa, it can be regulated or equalized
by simply raising or lowering the top or bottom
of the petticoat pipe. Sometimes this pipe is made
with openings and a kind of deflectors over them between
the two ends. It is then called a flounced petticoat
pipe, for obvious reasons.
No exact theory can be stated regarding the proportions
of these pipes, or the results effected by them,
which can be determined only by practical experience.
Some more accurate knowledge concerning them is,
however, much needed.
PART VIII. THE BOILER ATTACHMENTS.
Question 123.How is water supplied to the boiler to
replace that which is converted into steam?
Answer. It is usually forced into the boiler against
the steam pressure by force pumps, but another instrument
called an injector is now much used.
Question 124.What is the form of construction and
principle of the operation of such force pumps?
Answer. The ordinary single-acting force pump, fig.
66, used on locomotive and other steam engines
consists of a pump-barrel, A A, which is a cast-iron or
brass cylinder in which a tight-fitting piston, B B,
called the pump-plunger, works. This piston or
plunger is simply a round rod which works air-tight
through what is called a stuffing box, C, whose construction
will be fully explained hereafter. The
plunger receives a reciprocating motion, usually from
the piston-rod of the engine, but is sometimes worked
by a small crank attached to one of the crank-pins, or
by an eccentric on one of the axles. The pump-barrel
is connected with the water-tank of the tender by the
suction-pipe, D, and with the water-space of the boiler
by the feed-pipe, E E. Over the suction-pipe D is a
valve, F, called the suction-valve, which opens upward,
and below the feed-pipe, E, is another valve, G, called
the pressure-valve. These valves are cylindrical and
made of brass, and rest on brass seats, g, g, to which
they are fitted so as to be water-tight. They work in
guides, k, k, called cages, the form of which is more
clearly shown in the section, fig. 67, and the plan, fig.
68. When the plunger is drawn out of the pump-cylinder
it creates a vacuum behind it, and the pressure
above the valve G closes it, while the atmospheric
pressure on the water in the tank forces it into the
suction-pipe, opens the valve F, and fills the pump-cylinder.
When the plunger is forced back again the
force with which it presses against the water in the
pump-barrel, A, closes the valve F, and opens the
pressure-valve G, and the water is then forced through
the feed-pipe into the boiler. In order to be certain
that the water in the boiler will not flow back into the
pump, and also to prevent all the water and steam in
the boiler from escaping in case of accident to either
the feed-pipe or pump, another valve, H, fig. 66, called
a check-valve, is placed between the feed-pipe and the
boiler. The construction of this valve is similar to
that of the pressure and suction valves. It is inclosed
in a cast-iron or brass case, I I. All of these valves
have cages in which they work and which also act as
stops, which prevent them from rising from their seats
further than a certain distance. This distance is called
their lift, and the successful working of the pumps depends
very much on the amount of lift which the
valves have. This is usually from ³⁄₁₆ to ¹⁄₂ inch.
Fig. 66.
Fig. 67.
Fig. 68.
Over the pressure-valve G is a chamber, J, called an
air chamber. When water is forced into this chamber,
it is obvious that as soon as it rises above the
mouth of the pipe E, the air above the surface, c d, of
the water will be confined in this chamber. This
confined air, being elastic, will be compressed and expanded
by the pressure of the water, so that it forms
a sort of cushion, which relieves the pump and the
pipes from the sudden shocks to which they are subject,
owing to the rapid motion of the pump-plunger.
Another air-chamber, K K, is sometimes placed below
the suction-valve F. The object of this is to supply
a cushion to relieve the suction-pipe from the
shock which is caused by the sudden arrest of the motion
of the water in the pipe when the valve F is
closed. When the pump-plunger is drawn out, the
water flows through the valve F to fill the vacuum in
the pump-barrel, A A, and consequently all the water
in the suction-pipe is put in motion. As soon as the
plunger returns, the valve F is closed and the motion
of the water is suddenly arrested, thus producing more
or less of a shock in the pipe D. When the water in
the air chamber K K rises above the line a b, it is
evident that the air above that line will be confined in
the space surrounding the pipe L. This air then forms
a cushion in the same way as that in the upper air
chamber J does, which has already been explained.
The advantages of the lower air chamber are, it is
thought, more imaginary than real.
Question 125.How can the pump be taken apart
and the valves examined?
Answer. By removing the bolts e, e, the upper air
chamber can be taken off, and by taking out the bolts
f, f, the lower one can be taken down, and the valves
and cages removed. The check-valve H can be taken
out by removing the bolts l, l, which hold up the valve-seat
h and the valve and cage.
Question 126.How can it be known whether the
pump is forcing water into the boiler?
Answer. To show this a cock, called a pet-cock, is attached
to the upper air chamber in the position shown
by the dotted circle m.[33] By opening this cock, if the
pump is working, a strong jet of water will be discharged
from it during the backward stroke of the
pump-plunger. If the pump is not forcing water into
the boiler, or is working imperfectly, the stream discharged
from the pet-cock will be weak, and the backward
and forward strokes of the plunger will thus not
be very definitely indicated by the discharge from the
pet-cock.
[33] The pet-cock is sometimes attached to the feed-pipe.
Another small cock is often attached to the lower
air chamber, or to the feed-pipe, to allow the water to
escape from the pump in cold weather, when the engine
is not working, so as to prevent it from freezing.
Question 127.Why is it necessary to be able to regulate
the quantity of water which is forced into the boiler
by the pumps?
Answer. Because when the engine is working hard,
that is, pulling a heavy load up a grade, more steam
and consequently more water are consumed than when
it is not working so hard, and therefore more water
must be forced in to supply the place of that which is
used in the form of steam. If more water is forced in
than is consumed, the water will rise and fill the
steam-space and a part of it will then be carried into
the cylinders without being evaporated. If too little
water is forced into the boiler, the heating surface
will not be covered, and there will consequently be
danger that those portions which are exposed to the
fire will be overheated and injured.
Question 128.How is the supply of water which
is fed into the boiler by the pump regulated?
Answer. By a cock in the suction-pipe called a feed-cock,
which can be regulated by the locomotive runner,
so that more or less water is supplied to the pump.
There is also a valve in the water tank by which the
supply of water can be regulated.
Question 129.On what part of the locomotive are
the pumps usually placed?
Answer. They are usually attached to the frames
behind the cylinders, and are worked by the piston-rod,
as will be more fully explained hereafter; but
they are sometimes placed inside of the frames, that
is, between the wheels, and worked from an eccentric
on one of the axles, and sometimes they are placed
outside of the wheels near the back part of the locomotive,
and worked from short cranks attached to
the crank-pins.
Question 130.What provision is made for preventing
the water in the pumps from freezing in cold weather?
Answer. Pipes which communicate with the steam-space
of the boiler are attached to each of the suction-pipes,
so that, by opening valves in the former, steam
is admitted into the suction-pipes to heat the water in
them. By admitting this hot water into the pump, it
is kept warm, and the water is thus prevented from
freezing.
Fig. 69.
Question 131.What is an “injector”?
Answer. It is an instrument in which a jet of steam
from the boiler mingles with and forces a continuous
jet of water into the same boiler against its own pressure.
Question 132.What is the action of the injector and
what are the names of its essential parts?
Answer. All injectors have certain parts in common.
These may be shown in the simplest form of
instrument, as in the fixed-nozzle injector, a section of
which (omitting all detail of construction) is shown in
fig. 69.
The steam from the boiler, passing through the pipe
A, enters the receiving-tube C. Here it is joined by the
water which enters the pipe B. The water condenses
the steam in the combining-tube D, and a water jet is
formed which is driven across the overflow space F F,
and enters the delivery-tube H, thence past the check-valve
I into the boiler. During the passage of the
water from D to H, as it passes across the overflow
space F, if too much water has been supplied to the
steam, some will escape at this point and flow out
through the overflow nozzle G, while
if too little water has been supplied,
air will be drawn in at G, and carried
into the boiler with the water. The
names of the essential parts seem
very applicable when we notice that
steam is received from the boiler at
C, combines with the water at D, and
both are delivered to boiler through H.
Question 133.How is the operation
of the injector explained?
Answer. Steam escaping from under
pressure has a much higher velocity
than water would have under
the same pressure and condition.
The escaping steam from the receiving-tube
unites with the feed-water in
the combining-tube, and gives to this
water a velocity greater than it would
have if escaping directly from the water-space in the
boiler. The power of this water to enter the boiler
comes from its weight moving at the velocity acquired
from the steam, and it is thus enabled to overcome the
boiler pressure.
This can be illustrated with a wooden croquet ball,
which will float on the surface of water and will require
considerable force to make it sink. If, however,
it is thrown violently into the water, it will sink to a
considerable depth before its buoyancy will overcome
its momentum, or actual energy. If, however, we were
to take a very light, hollow wooden or india-rubber
ball, no matter how violently we throw it into the water,
it will not sink, because the total actual energy of any
body IS PROPORTIONAL TO ITS WEIGHT MULTIPLIED
BY THE SQUARE OF ITS VELOCITY, and therefore if
we throw the hollow ball at the same velocity as the
solid one, the former will still have much less energy
than the latter. Now, as already stated, steam under
a given pressure escapes from an orifice with a very
much greater velocity than water. But steam being
very light, if its weight is multiplied by its velocity
its total energy will be comparatively small. Now in
the injector, a portion of the high velocity of steam
is imparted to the heavy water, because this water
is presented to the action of the steam, not in a
mass, as in the boiler, but in small quantity and in
such a position that it can easily escape, so that it
gradually acquires as high a velocity as the escaping
steam can impart, and at the same time the steam
is condensed, and therefore there is a heavy substance
with a high velocity, whose actual energy is sufficient
to overcome the pressure in the boiler. If the steam
were not condensed we would have a comparatively
light substance moving at a high velocity, which, as
has already been explained, would have little actual
energy, and would therefore not overcome the boiler
pressure.
Question 134.Does this involve any principle like a
perpetual motion, or of work done without consumption of
power?
Answer. No, the steam escapes as steam, and is returned
to the boiler as water with its bulk reduced, say
1,000 times, and if it carries with it twenty times its
weight of fresh feed-water, there would still be a loss
of pressure or effective force in the boiler sufficient to
do the work required in introducing the water.
Question 135.Will the injector feed hot water?
Answer. The instrument will not work when the
feed-water is too hot to condense the steam, for the
reasons given above, and the amount of water thrown
is always the greatest when the feed-water is the
coldest. Steam at a low pressure can be condensed
more readily than steam of higher pressure, because it
contains less heat. The feed-water may be used hotter
to condense low steam than to condense high
steam. In using the injector, the lower the boiler
pressure the hotter may be the water within certain
limits, the limit being the possible condensation of the
steam.
Question 136.Will a “fixed-nozzle” injector, such
as has been described, answer as a boiler feeder on locomotives?
Answer. It will answer at some one pressure of
steam, to which pressure it may have been adapted in
making the instrument, and at that pressure it will
work admirably; but it will not work satisfactorily at
any other pressure, either higher or lower, and has
not much range in quantity of water delivered.
Question 137.What is required to make an injector
work at different pressures?
Answer. The instrument must be so made that the
water passage between the receiving tube and the
combining tube can be varied in size. This is usually
done by making the combining and receiving tubes
conical and moving the former to or from the latter,
thus contracting or enlarging the water space. Such
adjustment must be made at each change of steam
pressure in the boiler. If this adjustment is made by
hand, as in some kinds of injectors, it requires constant
attention, if the steam pressure varies frequently.
Question 138.How has this regulation been accomplished
without such attention?
Answer. In the SELF-REGULATING INJECTOR, fig.
70, by using the escape water at overflow to push the
combining tube towards the receiving tube and the indraught
of water at the same place to pull the combining
tube away from the receiving tube. This can
be explained as follows:
The case G of the instrument has two inlets, one
for steam, the other for water, the two being separated
by the plate F F. Steam passes into the
receiving tube A, and its escape is regulated by a
taper-plug in the end of the rod B, moved by the
handle H. At the upper end of the combining
tubeC, where it swells out into a bell mouth, is a
piston N N, sliding in the case. The lower end at
C is guided by the upper end of the delivery tubeD.
The delivery tube D is stationary. The overflow
opening is at O. The action of this instrument may
be thus described: Steam entering the receiving tube
A escapes through its lower end when the plug B
has been drawn back. It unites with the water surrounding
it in the space N N, is condensed and passes
with the feed-water into the delivery tube D, and
thence into the boiler. If too much water enters the
combining tube, some will escape at the overflow O,
and filling the space below the piston N N, will force
the combining tube up toward the receiving tube,
and, thus contracting the space between them, will
diminish the water supply; while, if it gets too little
water in this space, it will take some in at the overflow
O, and thus draw down the piston N N, and
enlarge the space, giving more water to the instrument.
This self-regulating principle enables the instrument
to continue working efficiently, no matter
how much the steam pressure in the boiler varies.
Fig. 70.
Question 139.How do you start this kind of injector?
Answer. The instrument just described is the
latest form of self-regulating injector, manufactured
by Messrs. Wm. Sellers & Co., and is called by its
makers the Injector of 1876. It is started and stopped
by a simple movement of the lever H. This lever
H moves a cross-head I, on the guide-rod J; it
also, by means of stops T and Q, on rod L, opens
and closes the starting-valve K. In fig. 70 the instrument
is shown shut off, and with the starting-valve
K open. On the rod B are two valves, a
small one W and a larger one X. A stop or collar is
shown a short distance beyond the large valve X.
If the lever H be drawn back until this collar comes
in contact with the valve K, it will have raised the
valve W from its seat, and steam will escape through
a small passage in the centre of the conical regulating
plug. The steam so admitted is sufficient to lift
the water, which will then be driven through D, and
past the valve K, and escape at P. Drawing back
the lever H to the end of its stroke, after the water
has been lifted, the large valve X is raised, and the
lug on the lever H, coming in contact with the stop
T, on the rod L, the valve K is closed. The jet is
fully established and the water is driven into the
boiler. At the entire end of stroke of the lever H,
the latch V falls into notches on the rod J, when,
as the lever is moved forward toward the position
shown in fig. 70, this latch will click over the notches
and hold the lever in any desired position between
the maximum and minimum delivery.
Question 140.What attachments are needed besides
the instrument to render it effective?
Answer. A globe-valve should be placed in the
steam pipe leading to the injector, to be closed only
when there is occasion to remove the injector when
steam is up, and in cold weather, to prevent the condensation
of steam in the pipes at the end of its
trips. During all the working time of the injector,
this valve should be wide open.
Question 141.In what position, and in what location
on the engine should the injector be placed?
Answer. On the right hand side, high enough up
to have an air chamber below the injector, above the
top of the water in the tank when the latter is full.
Question 142.What is required to keep the instrument
in working order?
Answer. Constant use is better than occasional
use. Having two injectors on the same engine,
one on each side, the one on the runner’s side will
be used while running. The one on the other side
should be used when standing. All pipe connections
must be tight, so as to prevent the leaking of air.
The pipe carrying steam to the instrument should
be from such part of the boiler as will insure the use
of dry steam, and the waste pipe must not be contracted.
The instrument represented in the engraving
is the injector of 1876, manufactured by Messrs.
William Sellers & Co. of Philadelphia. Beside this,
Mack’s and several other kinds of injectors are now
used.
Fig. 71.
Scale, ³⁄₈ in. = 1 foot.
LIST OF PARTS DESIGNATED BY LETTERS OF REFERENCE
IN FIG. 71.
A, Furnace Door. B, B, Driving Wheels. C, Driving Axle. D, D, Suction Pipes. E, Ash Pan Damper. F, F, Foot Steps for getting on and off the Locomotive. G, G, Hand Holds for getting on and off the Locomotive. H, I, Cab. J, J, Doors in front of Cab. K, K, Windows in front of Cab. L, Steam Gauge. M, Spring Balance. N, Steam Gauge Lever. O′ O, Throttle Lever. P, Water Gauge. Q, Stand for Tallow Can. R, Drip Pipe for Gauge Cock. T′ T, Rod for operating Feed Cock. T′, Regulator for Feed Cock. U V, Reverse Lever. W, Whistle. X, Blow-Off Cock. Z, Z, Frames. a, a, Heater Cocks. a a′, Heater Pipe. b, Blower Cock. c, c, Oil Cups for oiling Main Valves. d, Handle for opening Valves in Sand Box. e, e, Handles for opening Pet Cocks. f, Handle for opening Cylinder Cocks. g, Whistle Lever. h′, Whistle Handle. h, Rod connecting Whistle Handle to Whistle Lever. j, Handle for left hand Feed Cock. m m, Lever for shaking Grate Bars. n, Bell Crank for opening front Ash Pan Damper. o, o, Check Chains. p, Pipe for carrying off water from Gauge Cocks. s, s, s, s, Gauge Cocks. w, Handle for opening Blow-Off Cock.
Question 143.How can the height of the water in
the boiler be known?
Answer. Two appliances are used by which the
height of the water in the boiler can be observed.
These are: 1. Gauge or try cocks. 2. The glass water
gauge.
Fig. 72. Scale ¹⁄₄.
Fig. 73.
Scale, 3 in. = 1 foot.
Every locomotive is provided with four or more
gauge-cocks, which are usually placed at the back end
of the boiler, where they can easily be seen and
reached. These cocks, s, s, s, s, are shown in fig.
71, which represents the back end of a locomotive,
and to which frequent reference will be made. They
are also shown on a larger scale in fig. 72, which represents
the end plate of the boiler in section. They
communicate with the inside of the boiler and are so
placed that one is three or four inches above the other.
The two upper cocks are placed above the point where
the surface of the water should be when the engine is
working, and the two lower ones below it, so that the
upper ones communicate with the steam space and
the lower ones with the water. When these cocks are
opened, if the water is at its proper height, steam is
discharged from the two upper ones, and water from
the two lower ones.
When a gauge-cock which communicates with the
steam space is first opened, it is usually filled with
condensed water, so that it should usually be kept
open for a little while until this water is discharged.
If the upper cocks are opened and continue to discharge
water, they indicate that there is too much water
in the boiler; on the other hand, if steam is discharged
when the lower cocks are opened, then there
is too little water in the boiler, and the heating surface
is in danger of being exposed to the fire without
being covered with water, and consequently overheated,
or as it is called “burned,” and so injured as to become
too weak to bear the strain to which it is subjected
by the pressure of the steam. There is then
great danger that the crown sheet may be crushed
down by the pressure of the steam above it, or that
the boiler may be exploded. Even if no accident
occur, the boiler is in great danger of permanent
injury from overheating when the water is allowed to
get too low.
Below the gauge-cocks s, s, s, s, fig. 71, an inclined
cylinder, R, called a drip-pipe, is placed with
openings to receive the water and steam which are
discharged from the cocks. This water is conducted
away by the pipe p.
The water-gauge, P, fig. 71, which is shown in section
in fig. 73, consists of an upright[34] glass tube, a a,
which is from one-half to three-quarters of an inch
in diameter, and from 12 to 15 inches long. The
glass is about one-eighth of an inch thick. At its
ends it communicates with the steam and water of the
boiler through brass elbows, b, c. The openings in
these elbows, which communicate with the boiler, are
closed by the valves or plugs, d, e, which are worked
by screws and handles, f, g. The glass tube, when it
is attached to the elbows, is made steam-tight by rubber
rings, which are pressed tight around the tube by
packing-nuts, h, i. The elbows are provided with the
valves, d, e, so that in case the glass tube breaks the
steam and water can be shut off, so as not to escape
through the elbows. The lower elbow is provided
with a blow-off cock, k, through which any sediment
or dirt which collects in the glass tube or elbows can
be blown out. When the valves in the upper and
lower elbows are opened the steam flows into the glass
tube through the upper one, and water through the
lower one, and the water assumes a position in the
glass tube on a level with the surface of that in the
inside of the boiler; that is, the position of the water
in the boiler becomes visible in the glass tube. On
account of the constant variations of the water in the
boiler, the column of water in the glass never remains
stationary, but plays up and down as long as the
boiler is working. But if the communication between
the glass tube and the boiler is closed, then the water
in the tube becomes stationary and the water gauge is
useless. In order that there may be no obstruction of
the glass tube by mud or dirt from the water, it must
be blown out often. To do this the lower valve, e, is
closed, and the blow-off cock, k, and the steam valve,
d, are opened. The steam pressure in the tube on top
of the column of water will force it out of the blow-off
cock, and the mud and dirt will be carried with it.
[34] Sometimes these tubes are, for convenience, inclined, as shown in
fig. 71.
If from any cause the glass tube is broken, first of
all the water-valve e should be closed and then the
steam-valve d, so as to prevent the hot water and
steam which will escape from the broken glass from
scalding those who are working the engine. By unscrewing
the nuts h and i the old glass can easily be
removed and a new one substituted in its place.[35] Care
should be taken in putting in new glasses not to screw
the packing nuts down any more than just sufficiently
to make the rubber rings steam-tight around the glass
tubes. If they are screwed too tight they are apt to
produce a strain on the tube, so that the slightest expansion
by heat or contraction from cold will break it.
[35] Extra glasses should always be carried with an engine so as to be substituted
in case of accident to the one in use.
Fig. 74.
Scale 1¹⁄₂ in. = 1 foot.
Fig. 75.
Scale 1¹⁄₂ in. = 1 foot.
Question 144.How is the steam pressure in boilers
prevented from exceeding a certain limit?
Answer. By what are called safety valves. These
consist of circular openings, a, fig. 74, about three
inches in diameter placed usually on the top of the
dome,[36] and covered by a valve,
b, which is pressed
down either by a lever, c c′, and spring, d, as shown in
fig. 74, or by a spring alone, as in fig. 76. Two of
these valves are usually placed on the top of the dome,
so that if one gets out of order the other one will allow
the steam to escape as soon as its pressure exceeds
that which, it has been decided, the boiler can safely
bear. This pressure, in locomotive boilers, is usually
from 100 to 130 pounds per square inch.
Question 145.How is the amount of pressure which
must bear on top of a safety-valve determined?
Answer. This pressure is determined BY MULTIPLYING
THE AREA OF THE OPENING FOR THE VALVE
IN SQUARE INCHES BY THE GREATEST STEAM PRESSURE,
IN POUNDS PER SQUARE INCH, WHICH THE
BOILER IS INTENDED TO BEAR. Thus, if the opening
for a safety-valve is three inches in diameter,
its area will be seven square inches, and, therefore, if
the greatest steam pressure which it is intended that
the boiler shall bear is 100 lbs. per square inch,
the valve must be pressed down with a pressure
equivalent to 7 × 100 = 700 pounds. If the pressure
on the valve is produced by a lever, as in fig. 74,[37]
then the total weight of the safety-valve must be
MULTIPLIED BY THE SHORT ARM OF THE LEVER,
(or the distance A between the centre of the fulcrum
e and that of the load f,) AND DIVIDED BYB, THE
TOTAL LENGTH OF THE LEVER. In fig. 74 the short
arm of the lever is 3¹⁄₂ inches, and the whole length
35 inches; therefore if the valve is to be pressed down
with a pressure of 700 pounds, the pressure on the end
of the lever would be calculated as follows:
700 × 3¹⁄₂35 = 70 lbs.
[37] The lever is represented in the engraving with a piece broken out, in
order to save room.
The spring d must therefore pull down on the end
of the lever with a tension equal to 70 pounds. When
the pressure of the spring bears directly on the
valve, as shown in fig. 76, then the tension of the
spring must be just equal to the pressure on the valve.
This tension is produced by screwing down the nuts,
c, c. The spring d, which produces the requisite
pressure on the end of the safety-valve lever, fig. 74,
is arranged inside of two cylinders, g and h, which
slide over or into each other like the sections of a telescope.
This arrangement is called a spring-balance.
The spring, d, is attached to the covered ends and
draws them towards each other. The upper cylinder
g is connected by a rod, i, to the flattened end of the
lever c′, which has a hole drilled through it to receive
the rod. The other end of the rod is screwed into the
upper cylinder g. This rod is sometimes arranged so
that it can be either lengthened or shortened by the
nut j. By lengthening or shortening the distance,
the tension of the spring is either diminished or increased.
The lower cylinder of the spring-balance,
represented in fig. 74, is attached to a lever, m, which
is fastened to the back of the steam-gauge k. This is
shown more clearly by fig. 75, which represents the
back of the gauge, and also the lever, l m, whose fulcrum
is at m. The spring-balance is attached to the
lever at k. By drawing down the lever the tension of
the spring is increased, and by raising it up it is diminished.
The lever is held in any desired position
by the latch, n, and the ratchet r r. By this contrivance,
which is employed on the engines built at the
Grant and also at the Baldwin Locomotive Works,
the pressure on the valve can at once be either increased
or diminished, which it is often desirable to
do, especially when an engine is not at work. The
spring-balance is shown in fig. 71, and is indicated by
the letter M and the lever by N. Unless the pressure
of the steam exceeds that on top of the valve, it
will of course not be opened. As there is always danger
that a safety-valve or some of its attachments
may become corroded or otherwise disordered, so that
it will not act promptly or with certainty, it is desirable
to open it frequently, so as to be sure that it is
in good working order. To do this the pressure on
the valve must be reduced below that in the boiler,
which can very conveniently be done with the spring-balance
lever which has been described.
The lower cylinder of the spring-balance sometimes
carries an index or pointer, t, fig. 74, which protrudes
through a slot in the cylinder g, and indicates the
amount of pressure of the spring on a scale marked
along the slot on the outside of the cylinder. If it is
desired that the safety-valve should open when the
steam pressure reaches 100 or any other number of
pounds per square inch, the spring-balance is subjected
to a tension which will bring an amount of pressure
on the top of the safety-valve equal in pounds per
square inch of its surface to that of the steam pressure
desired.[38]
[38] In loading a safety-valve allowance must always be made for the
weight of the lever and the valve.
There should always be some provision made which
will render it impossible to increase the steam pressure
beyond that which it has been determined that
the boiler will safely bear. This is usually done by
arranging one of the safety-valves with a lever, as
shown in fig. 74, and the other without, like that in
fig. 76. The latter is often covered and sealed or locked
up, so as to be beyond the control of the locomotive
runner.
The safety-valves are usually fitted into conical
seats, S S, figs. 74 and 76, so as to be perfectly steam-tight,
and are made with wings or guides, t, t, the
form of which is shown in the sectional plan A, figs.
74 and 76, under the valve. These guides are intended
to keep the valves in the proper positions in
relation to their seats.
Fig. 76. Scale ¹⁄₈.
As soon as the steam pressure under the valves becomes
greater than the pressure of the springs on top
of them, the valves will be lifted up and the steam
will escape until the pressure in the boiler is relieved.
It will be seen, however, that although the surface of
the valve which is exposed to the pressure of the
steam is equal to the area of the opening for the valve,
after it is lifted from its seat and the steam escapes
all around the edge, a larger surface will be exposed
to the pressure of the escaping steam. For this reason,
it will be found that after a valve is opened steam
will escape, or “blow off,” as it is termed, until the
pressure is several pounds lower than it was when the
valve first opened. Advantage has been taken of this
fact in the valve shown in fig. 76, which is called the
“Richardson” valve, which is now much used. The
top of this valve is made larger in diameter, so as to
expose more area to the escaping steam. Grooves
are also made around the edge of the valve and the
seat. These, it is claimed, produce some sort of reflex
action of the steam, which keeps the valve open longer
than it otherwise would be.
Fig. 78.
Fig. 77.
Question 146.How is the steam pressure in the boiler
indicated?
Answer. By an instrument called a steam-gauge.
There are a great variety of such instruments made,
but they may all be divided into two classes, and
they all operate upon one of two principles. In the
one class the pressure of the steam acts upon a diaphragm
or plate of some kind, as shown in fig. 77,
which represents a section of a gauge of this kind;
a b is a metal plate made with circular corrugations,
as shown in section and also by the shading in fig. 78,
which represents a front view of the gauge with a part
of the dial-plate removed. The steam enters by the
pipe c and the small opening d, and fills the chamber
e behind the metal plate or diaphragm. The corrugations
of the latter give it sufficient elasticity, so that
when the pressure is exerted behind it, it will be pressed
outward by the steam. If it were flat, it is plain that
it would not yield, or only to a very slight degree, to
the pressure of the steam. In the centre of the diaphragm
on the outside is a pin or stud, f, which bears
against the plate. This stud is attached to a bent
lever or “bell-crank,”[39]g h k, whose fulcrum is at h.
To the outer end, k, a rod, l, figs. 77 and 78, is attached,
the lower end of which is connected to the
short arm m of a toothed segment, n, whose fulcrum is
at o. This segment gears into a small pinion, p, which
is attached to a spindle or shaft, which carries a pointer,
fig. 78. It is obvious now that if the diaphragm,
a b, is pressed outward, it will move the bent lever
k h g, the motion of which will be communicated by
the rod l to the toothed segment n, which will in turn
revolve the pinion p, and thus move the hand or index.
We have selected for this illustration one of many
forms of this kind of gauge. The mechanical appliances
for communicating the motion of the diaphragm
to the index or pointer are different in the gauges
made by different manufacturers. The form of the
diaphragm also differs. In some cases it is made of
a metal plate; in others a spiral spring is used, covered
with india-rubber to make it steam-tight. The
steam-gauge represented by figs. 77 and 78 is the
form manufactured by M. B. Edson, of New York.
In the other class of gauges, shown in fig. 79, the
steam acts upon a bent metal tube, a b c, usually of a
flattened or elliptical section. It may not be known
to all readers that if a tube bent, say in the form of
the letter U or C, is subjected to the pressure of a
liquid or gas on the inside, the force exerted by the
pressure has a tendency to straighten out the tube.
This is due to the tendency which a tube of an elliptical
or flat section has to change the shape of the latter
and approximate to a circular form when the inside
is subjected to a pressure. Thus let A B, fig. 80,
represent a cross section, and a b d c, a longitudinal
section of a part of such a tube contained between
two radii, O a and O b, drawn from the centre O of
the curve in which the tube is bent. If now we subject
the inside of A B to a pressure it will have a tendency
to assume the form of the circle C D, and
would then be represented in the longitudinal section
by the dotted lines a′ b′ d′ c′. If now we draw
radial lines through a′ c′ and b′ d′, it will be found
that they intersect at O′, instead of O, which was the
original centre of the curve of the tube. It will be
seen that as the section of the tube approximates to
the form of a circle, the portion a b which is outside
the curve will be moved farther from the centre,
while the other side, c d, is moved nearer to it. As
indicated by the radial lines, when this occurs either
the outside must be lengthened and the inside shortened,
to conform to the radial lines a O and b O, or
else the tube will be straightened so that the radial
lines will assume the position a′ O′ and b′ O′.
The phenomenon of the straightening of the bent
tubes of steam gauges is frequently attributed to the
difference between the area of the inside and outside
of the curve. This error was shared by the writer,
until the fallacy of the reasoning which supported it
was pointed out to him.
In the gauge represented in fig. 79, (in which the
dial-plate is removed), one end, c, of the tube is attached
at d to a lever which has a toothed segment, e, at
the other end. The end a of the tube is connected
with the lever at f. The connection at d, therefore,
forms the fulcrum of the lever. It is obvious that as
the two ends of the bent tube are forced apart by the
steam pressure, the lever and the segment have motion
imparted to them. The latter gears into a pinion on
the spindle of the index or pointer, r r, which thus
indicates on the dial the degree of pressure in the
tube. The latter is connected with the boiler by a tube
attached at g. Various forms of this kind of steam-gauge
are also made, but all act on essentially the
same principle.
The position of the steam-gauge on the engine is
shown at M, in fig. 71.
Question 147.Why is the pipe which connects the
steam-gauge with the boiler bent as shown in fig. 71?
Answer. To prevent the hot steam from coming in
contact with the metal plate or tube, as it is found
that the heat of the steam affects their elasticity.
When a bent tube is used, the steam from the boiler
is condensed and fills the bent portion so that when
the steam pressure comes on the surface of the water
it forces it up the other leg of the tube into the gauge.
A cock is attached to this pipe so that the steam can
be shut off in case the gauge should get out of order
or require to be removed while there is steam in the
boiler.
Question 148.How can the accuracy of a steam-gauge
be tested?
Answer. When the gauge is in good working order,
the index or pointer moves easily with every change
of pressure in the boiler, and if the steam is shut off
from the gauge, the index should always go back to 0.
In order to determine the accuracy of its indications,
however, they should be tested with a column of mercury.
This consists of a long, vertical tube, terminating
at its base in a closed vessel filled with mercury.
The gauge is then attached to the top of this vessel
and water or oil is forced into the vessel on top of the
mercury and into the gauge. A pressure of one
pound per square inch will force up the column of the
mercury 2.04 inches, so that by graduating the tube
into spaces that distance apart, the divisions will indicate
the pressure in pounds per square inch. Thus, a
pressure of 50 pounds would force up the column of
mercury 102 inches, and with 100 pounds pressure
the column would rise 204 inches, and therefore,
when the mercury reaches these or any other points,
the steam-gauge, if it is accurate, should indicate
equivalent pressures.
The ordinary steam-gauges are very liable to get
out of order, and therefore they should be frequently
tested to ascertain whether their indications are
correct.
Question 149.What is the steam whistle, and for
what purpose is it used?
Answer. The steam-whistle, W, fig. 71, and shown in
section on a larger scale in fig. 81, consists of an inverted
metal cup or bell, A, made usually of brass.
The lower edge of this cup is placed immediately
over an annular opening, a a, from which the steam
escapes and strikes the edge of the cup or bell, which
produces a deep or shrill sound, according to the size
or proportions of the whistle. The annular opening
a a is formed by the plate or cover, a a, which nearly
fills the mouth of the cup B, which is attached to the
stem c. The latter is screwed into the top, D, of the
dome. Communication with the steam-space of the
boiler is either opened or closed by a valve, b, which is
attached to a sort of spindle, d, which extends upward
inside of the stem c. This spindle does not entirely
fill the opening in the stem c, so that the steam which
enters when the valve b is opened rises and escapes
through the holes e, e, e, into the cup B and out
through the annular opening a a. The valve is opened
by the lever E, whose fulcrum is at f. The end g of
this lever is connected by a rod, h, figs. 81 and 71,
with the cab, and by a suitable handle or lever, h′ h′,
fig. 71, it can be opened and the whistle be blown
at any time by the locomotive runner or fireman to
give signals to the trainmen or of the approach of a
train to a station, or to warn persons to get off of the
track.
Fig. 81. Scale 1¹⁄₂ in. = 1 foot.
Question 150.How is a locomotive boiler emptied
and cleaned?
Answer. One or two large cocks, called blow-off
cocks, X, fig. 71, are placed near the bottom of the fire-box,
either in front or behind, and sometimes on the
side. By opening either of these the water in the
boiler is blown out, and much of the loose mud and
dirt is carried out with the water. The cock X, fig.
71, is opened by a handle, w, which is connected with
the cock by a rod.
In order to clean out the mud and scale which are not
entirely loose, what are called mud-holes or hand-holes
are placed in the corners of the fire-box near the bottom.
These are oval-shaped holes, about 4¹⁄₂ inches
long and 2¹⁄₂ inches wide, and covered with two metal
plates, one of which is put inside the boiler and the
other outside, and fastened with a bolt through both.
Another hand-hole is sometimes placed in the bottom
of the front tube-sheet. When the boiler is emptied
of water these hand-holes are uncovered, and as much
dirt is removed as can be scraped out of these holes.
A hose pipe is then inserted and a strong stream of
water is forced in, which washes out nearly all the
loose dirt, so as to leave the boiler comparatively
clean.
When the water is very impure, what is called a
mud-drum, M, fig. 41, is used. Much of the mud and
dirt is deposited in this receptacle, from which it can
easily be removed by taking off the cast-iron cover on
the bottom of the drum. The cover is also provided
with a blow-off cock, which is shown in the figure referred
to.
Question 151.What other attachments are there to
the boiler of a locomotive?
Answer. There are two cocks, a, a, fig. 71, called
heater-cocks, which are connected with pipes to the feed-pipes
D D, to admit steam to the latter to prevent the
water in them from freezing. There is also another
cock, b, called a blower-cock, which is connected to the
smoke-stack by a pipe b, b. Steam is conducted through
this pipe and escapes up the chimney in a jet, thus producing
a draft when the engine is not working. This
arrangement is called a blower and is used to blow the
fire when the engine is standing still. The action of
the jet is similar to that of the exhaust steam which
escapes up the chimney, excepting that the steam from
the jet escapes in a continuous stream instead of distinct
“puffs,” as it does when it is liberated alternately
from one end of the cylinders and then from
the other.
T′ is a handle which is connected by a rod, T′ T,
with the feed-cock (not shown in the engraving) in
the pipe D. This cock can be opened or closed by the
handle, and the supply of water fed into the boiler by
the pump can thus be regulated. J is a handle on the
other side of the engine, for regulating the working of
the pump on that side.
e, e are handles, also connected by rods with the
pet-cocks on the pumps. These cocks can thus be
opened or closed, and it can then be known whether the
pumps are working.
A is the furnace door, which is fastened by a latch.
The latter has a chain, Q, attached to it by which it
can be conveniently opened or closed. The door also
has a circular register with six holes to admit air into
the furnace. These holes can be opened or closed by
the revolving circular disc shown in the engraving.
Fig. 82. Scale ³⁄₄ in. = 1 foot.
Fig. 83. Scale ³⁄₄ in. = 1 foot.
Fig. 84. Scale ³⁄₄ in. = 1 foot.
Question 152.How are the grates constructed?
Answer. As has already been explained, they are
made usually of cast-iron bars,[40]A, A, A, figs. 82 and
83, called grate-bars. Fig. 82 is a plan, and fig. 83 a
horizontal section of one form of grate. The bars in
this kind of grate are usually cast in pairs, or some
times three or more are cast together. They are made
wider on the top than on the bottom edges, as shown
in the section, fig. 83, so that cinders and ashes will
fall through easily, and also to give free access to the
air from below. They are usually from ³⁄₄ to 1¹⁄₂ inches
wide on the top, and about ³⁄₄ inch on the lower
edges. The spaces between the bars are made from ¹⁄₂
to 1¹⁄₄ inches wide. For burning wood the bars are
placed comparatively close together and are stationary,
but for burning bituminous coal they are usually
made so that they can be moved, in order to shake or
stir up the fire, just as is necessary in an ordinary
stove or grate fire. In the grate we have illustrated
the bars, A, A, are cast in pairs, and run crosswise of
the fire-box. The ends are made with a sort of journals,
b, b, which rest on two supports, B, B, called
bearing bars, which have suitable indentations to receive
the ends of the grate-bars. The latter have
arms, C, C, fig. 83, cast on the under side, to which a
bar, D D, is attached. By moving this bar back and
forth, the grate-bars have a rocking motion imparted
to them, as shown in fig. 84. It is evident that in
this way the fire over the whole surface of the grates
will be disturbed or shaken. The bar, D D, is moved
by a lever, m m, shown in fig. 71. An extension
piece, not shown in fig. 71, is used with the lever m m,
so as to increase its length; but it is removed after it
has been used, so as not to be in the way of the fireman.
Grates which have movable bars are called
shaking or rocking grates. A great variety of such
grates are made and in use, to describe which would
require more room than is available here.
[40] In Europe and in some few cases in this country they are made of
wrought iron.
For burning anthracite coal what are called water-grates
are used. These consist of wrought-iron tubes,
2 inches in diameter outside, which are fastened in
the front and back plates of the fire-box and are inclined
upward from the front end, so that there
will be a continued circulation of water through them
to keep them cool and thus prevent them from being
burned out by the intense heat of the fire.
Question 153.How is the fire removed from the fire-box
when it is necessary to do so?
Answer. In bituminous coal burning engines, what
is called a drop-door, E E, figs. 82, 83 and 84, is provided
for that purpose. This door is supported partly
on journals, d, d, similar to those in the grate-bars, on
which it can turn, and is held up or prevented from
dropping by arms, e, e, attached to a shaft, F F. This
shaft is operated by a lever, f f, fig. 82, outside the
fire-box.
When the arms are in the position represented in
fig. 83, the drop-door is held up in the place in which
it is shown; but when they are turned as in fig. 84, the
door falls down so that the burning coal can be taken
out of the opening at G, and, by raising up the ash-pan
damper, H, fig. 84, can be raked out on the track
or into suitable pits usually provided for this purpose.
The drop-doors are sometimes perforated so as to admit
air to the fuel on top of them.
The grates for burning anthracite coal usually have
about four solid wrought-iron bars between that number
of tubes. These bars can be withdrawn, and the
fire then falls into the ash-pan through the opening
left by the withdrawal of the tubes.
Question 154.How are the dampers of the ash-pan
operated?
Answer. They are connected by suitable rods and
levers with two handles, l, l, fig. 71, which are raised
or lowered, thus opening or closing the dampers.
PART IX. THE THROTTLE-VALVE AND STEAM PIPES.
Question 155.How is the steam admitted to and the
supply regulated or shut off from the cylinders?
Answer. By a valve, h, fig. 41, called a throttle-valve,
which is usually placed at the end of the pipe I, near
the top of the dome. Throttle-valves are sometimes
placed in the smoke-box at the front end, n, fig. 41, of
the dry-pipe. Until within a few years they consisted
of plain slide-valves which covered openings similar
in form to the steam-ports, but smaller in size. The
pressure on such valves is of course greatest when
there is no steam underneath, which is the case when
the valves are closed. It is then very difficult to open
them, and as it is important that the supply of steam
admitted to the cylinders when the locomotive is started
should be easily regulated, such valves are objectionable,
and therefore the form has been introduced which
is illustrated in fig. 41, and also on a larger scale in
fig. 85, which represents a longitudinal section of the
throttle-pipe and valve. This is what is called a
double-poppet valve, and consists of two circular discs,
a and b, which cover two corresponding openings in
the end of the pipe I. When these discs are raised
up, as shown in fig. 85, steam flows in around their
edges, as represented by the darts. It will be observed
that the steam pressure in the boiler comes on
top of the disc a and against the under side of b. The
pressure on the one thus neutralizes or balances that
on the other. If the two discs were of the same size,
the pressure of the one would be exactly the same as on
the other; but as they are joined together and are
made to fit steam-tight on their seats by what are
called countersunk joints, their diameters must be somewhat
larger than the openings they cover. The only
practicable way, therefore, by which the lower disc b
can be introduced into the end h of the pipe I so as to
cover the lower opening is through the upper opening
a. For this reason the lower disc must be made
smaller than the upper one, and therefore the
pressure on the upper one, being in proportion to its
size, has a constant tendency to close the valve. As
it is of the greatest importance that a throttle-valve
should remain closed after steam is shut off, and never
be opened at any time accidentally, the arrangement
described accomplishes just what is needed—that is,
makes the valve work comparatively easily, and at the
same time keeps it closed after the steam has been
shut off.
Fig. 85. Scale ³⁄₄ in. = 1 foot.
Fig. 86. Scale ³⁄₄ in. = 1 foot.
Question 156.How is the valve opened and closed?
Answer. By a lever, O′ O, called a throttle-lever, figs.
85, 86[41]
and 71. This lever is connected by a rod, d,
called the throttle-stem, with a bell crank, i, the other
arm of which works the rod c, to which the throttle-valve
is attached. The rod d works through a steam-tight
stuffing-box, f, in the back end of the boiler.
The end of the throttle-lever is attached to two links,
g, fig. 86, which are fastened by a pin to the stud h.
These links have a slight vibratory motion, which
enables the pin k, by which the lever O′ O, is fastened
to the rod d, to move in a straight line, which is
necessary in order that the rod d may work steam-tight
in the stuffing-box, f. The throttle-lever has a
latch, l, which gears into a curved rack, n, so as to hold
the lever and valve in any required position. This
latch is operated by a trigger, m. Various other devices
are used to fasten the throttle-lever and thus
hold it in any position required.
[41]Fig. 86 is a plan, showing the top of the valve and lever.
Question 157.How are the steam pipes constructed?
Answer. The steam, after it is admitted by the
throttle-valve, as was explained in answer to Question
155, passes into the throttle-pipe I and the dry-pipe
m m, fig. 41. At the front end of the dry-pipe a pipe,
n, figs. 40 and 41, which divides into two branches
like the top of the letter T and is therefore called a
T-pipe, is attached. The steam-pipes o, o, fig. 40, are
connected to each of the two branches of the T-pipe at
one end and to the cylinders at the other.[42]
[42] In fig. 40 the right-hand side represents a section through the steam-pipe
o o, and the left a section through the exhaust pipe e e.
Fig. 87. Scale 1¹⁄₂ in. = 1 foot.
Fig. 88. Scale 1¹⁄₂ in. = 1 foot.
These pipes, being in the smoke-box, are exposed to
great changes of temperature, and are therefore subjected
to expansion by heat and contraction by cold.
The joints are therefore constantly subject to disturbance
by the contraction and expansion of the pipes
and so are difficult to keep tight. It is also practically
impossible to construct the boiler, the cylinders and the
pipes with perfect accuracy, and therefore a small
amount of adjustability and flexibility is necessary in
the joints of the pipes. If, for example, the opening
x in the cylinder, fig. 40, were either too near or too
far from the cylinder of the engine, it would be necessary
to move the end of the pipe o either to the right
or to the left in order to connect it with x. If the
joint of the upper end of the steam-pipe were attached
to the T-pipe with a flat joint like that shown at a b,
fig. 87, it would be impossible to move the lower end
of the steam-pipe either to the right or to the left
without disturbing the joint and causing it to leak.
For this reason these pipes are connected with what
are called ball joints, fig. 88, that is, the end a b of one
of the pipes is turned into the form of a part of a
sphere,[43] and the other end into a corresponding concave
form. It is known that a sphere will fit into a
corresponding socket in any position; for example, an
acorn in its cup or the bones at the hip or shoulder
joints. If, therefore, the pipes are joined with such
spherical or ball-joints as they are called, the lower end
can be moved sideways several inches either way, and
the joint will still be steam-tight if it is then firmly
bolted together. Even after it is bolted together
it will have so much flexibility that the expansion
and contraction of the pipes will not cause it to leak.
[43] The dotted lines indicate what would be the form of the sphere if the
pipe was solid instead of hollow.
There is, however, still another difficulty. Although
the lower end of the pipe, o o, fig. 40, can, with a ball-joint
above, be moved in any direction horizontally,
yet if the pipe is too long or too short it is obvious such
a joint will not permit it to be moved up or down.
A joint with a flat surface, like that shown in fig. 87,
would, however, permit such motion in the pipe without
leaking. If, for example, the steam-pipe were ¹⁄₈
of an inch too short, it might be drawn down that distance,
and if the upper joint were then screwed up it
would still be steam-tight. In order, then, to get both
vertical and lateral flexibility in the joints of the
steam-pipes, a ring, a b, fig. 89, is interposed between
the pipes. One side of this ring is spherical and the
other flat, so that the pipes can move either around
the spherical part or slip up or down or sideways on
the flat surface of the ring. In this way the pipes are
flexible and adjustable in every direction, and for all
kinds of motion caused by expansion, or which may
be needed when the parts are put together. Sometimes
the joints at one end only of the steam-pipes are
made in this way, and the other is connected with a
simple ball-joint.
Fig. 89. Scale 1¹⁄₂ in. = 1 foot.
In designing these joints their form should be
drawn with a radius, c d, fig. 88, from one centre, c, so
that the surface of the joint will form a part of a
sphere. If they are drawn from two centres, as is
sometimes done, it is obvious that the surface of the
joint will not be a part of a sphere, and therefore will
not have the requisite flexibility. The surfaces of the
joints are carefully turned to the proper form, and
then made steam-tight by scraping or grinding them
with emery and oil, and the pipes are then fastened together
with bolts, g, g, fig. 89, and flanges, f, f, cast on
the pipes.
Question 158.How are the exhaust pipes constructed?
Fig. 90. Scale 1¹⁄₂ in. = 1 foot.
Answer. They are made of cast iron. When two
nozzles are used they are generally cast together, as
shown in fig. 90. When only one is used, the form of
the pipes resembles somewhat that of an inverted letter
⅄, as shown in fig. 91, so as to cover the two openings
which connect with the cylinders. The tops of
these pipes have rings or bushings, a a, fitted into
them, which are held by set screws, b, so that they can
easily be removed and others with larger or smaller
openings be substituted. If the openings in the
exhaust-nozzles are small, the steam must be discharged
at a higher rate of speed, in order to exhaust
all that is in the cylinders, than if the blast orifices
are larger. Therefore, if the latter are reduced in
size, the draft becomes more violent, but at the same
time the back-pressure in the cylinder (which will be
explained hereafter) is increased. It therefore becomes
necessary to adjust the size of the blast orifices
with the greatest care, so as to have them just small
enough to produce the required draft and yet leave
them as large as possible, so as to reduce the back-pressure.
For these reasons what are called variable
exhausts are sometimes used. In these the blast orifice
can be increased or diminished at pleasure, and thus
regulated to suit the conditions under which an engine
is working. A great variety of such devices has been
used, but now nearly all have been abandoned for the
simpler arrangement described, which is not variable
when the engine is working.
Fig. 91. Scale 1¹⁄₂ in. = 1 foot.
PART X. THE CYLINDERS, PISTONS, GUIDE-RODS AND CONNECTING-RODS.
Question 159.How are the steam cylinders constructed?
Answer. They are made of hard cast iron, and have
the steam and exhaust ports and valve-seats cast with
them. The harder the iron the better will the cylinders
withstand the wear of the pistons and valves, but
they must at the same time be made soft enough, so
that after they are cast the inside can be bored out
perfectly cylindrical, the ends turned off, the bolt-holes
drilled, and the valve-seats planed smooth.
Fig. 92 represents a longitudinal section through
the centre of the cylinder and steam-chest. Fig. 94
is a plan of the same parts with the cover of the steam-chest
and the valve removed. The left-hand side of
fig. 95 shows a transverse section through the centre
c d, fig. 92, of the cylinders, and the right side is a
section through the steam-pipe G h, fig. 94. The
same letters indicate like parts in the three different
views.
The cylinders of locomotives in this country are
now universally placed on the outside of the wheels,
as has already been described. In order to fasten
them securely together and to the boiler, they are attached
to what is called a bed-plate or bed-casting, D D,
figs. 94 and 95, which is placed between them. Some
builders make this bed-casting in a separate piece,
and the cylinders are then bolted to it on the outside,
about at the dotted lines, l, m, fig. 95. Others cast
one-half of it with each cylinder, as shown in our engravings,
and then bolt them together at the line i, j,
which is the centre of the engine. The bed-casting
is also bolted to the smoke-box by the flanges E, E.
The cylinders are bolted to the frame F with bolts, m
and k, fig. 95.
After the cylinders are bored out, and the ends
turned off, heads, A and B, figs. 92 and 94, are fitted
with steam-tight joints to each end. These heads
are fastened with bolts and nuts, a, a, a, to flanges,
C, C.
Question 160.How is the steam conducted to and
from the cylinders?
Answer. Two pipes or passages are cast in each cylinder,
the one, G G′, fig. 95, for admitting steam into
the steam-chest, and the other, H H′, for exhausting
it from the cylinders. The one G G′ is called the
steam-passage, and the other, H H′, the exhaust-passage.
The steam-passage terminates at one end with a round
opening, G, figs. 94 and 95, to which the steam-pipe
o, figs. 40 and 95, is attached inside of the smoke-box.
At the other end it divides into two branches,
G′, G′, fig. 94, each of which terminates in an opening,
g, g′, inside of the steam-chest. The steam is
thus delivered at both ends of the chest, and can pass
freely into each of the steam-ports. By making the
cylinders in this way, they are exactly alike for each
side of the engine, or, to use a shop phrase, there are
“no rights and lefts,” so that a cylinder casting can be
used for either side of the engine. This method of making
cylinders has been adopted by a number of the principal
builders in this country, but is by no means universal.
Fig. 92. Scale ³⁄₄ in. = 1 foot.
Fig. 93.
Fig. 94. Scale ³⁄₄ in. = 1 foot.
Fig. 95. Scale ³⁄₄ in. = 1 foot.
Question 161.How is the steam-chest constructed?
Answer. It usually consists of two castings, one of
which, J, figs. 92 and 94, is a square cast-iron box
made open at the top and bottom. This rests on the
top of the cylinder casting and is joined to the latter
with a steam-tight joint. On top of it is a cast-iron
cover, K K. The steam-chest and cover are held
down by bolts, p, p, which are screwed into the cylinder
casting and have nuts on top.
Question 162.How are the slide-valves made to work
steam-tight on the valve-seats?
Answer. They are first planed off smooth, and then
filed and scraped until the two touch each other over
the whole of their surfaces in contact. The valve-stem
v, fig. 92, works steam-tight through a stuffing-box on
the steam-chest.
Question 163.How are the valves and pistons oiled?
Answer. The oil is usually introduced into the steam-chest
through a cock, c, fig. 92, called an oil-cock.
From this cock it flows down upon the valve and is
conducted by suitable holes and channels to the
valve-face and from there through the steam-ports to
the cylinder and piston. Sometimes, for greater convenience,
oil-cocks c, c, fig. 71, are placed inside of the
cab and communicate by pipes with the steam-chests.
The valves are oiled by pouring oil or melted tallow
into the oil-cocks when the steam is shut off from the
steam-chests and cylinders. When the pistons are
working in the cylinders without steam, they create
a partial vacuum, so that if oil is then poured into
the oil-cocks it will be sucked into the steam-chests,
or, in other words, it will be forced in by the pressure
of the air above it. Q, fig. 71, is a shelf attached to
the boiler to receive an oil-can filled with oil or tallow,
which is thus melted or kept in a fluid condition by the
heat of the boiler.
Question 164.How are the cylinders and steam-chests
protected so as to prevent, as far as possible, the heat
in the steam from being lost?
Answer. The sides of the cylinders are covered with
wood, w, w, w, fig. 95, called the cylinder lagging, and
the wood is covered outside with Russia iron or brass,
which is called the cylinder-casing. The ends of the
cylinders have light metal covers, called cylinder-head
covers, made of cast iron, brass or sheet metal. The
steam-chest is covered in a similar way so as to be
surrounded either with a covering of wood or of confined
air. Sometimes coarse felt is used for the purpose.
The covering, excepting the cylinder lagging,
is not shown in the engravings.
Question 165.For what purpose are the cocks C, C,
figs. 92 and 95, at each end of the cylinder, used?
Answer. They are used to exhaust the water which
collects in the cylinders. When the engine is not
working the cylinders and steam-pipes are all cooled
off, so that when steam is first introduced into them
a great deal of it is condensed until they become
warmed. Water is also frequently carried over from
the boiler with the steam. When this occurs the
boiler is said to prime, or to “work water.” This water
and that produced by the condensation of steam collect
in the bottom of the cylinder and will not escape
through the exhaust-pipes until the piston moves up
so near to the end of the cylinder that the water will
fill the whole space between it and the cylinder-head.
As has already been stated, it will then escape so
slowly that the momentum of the piston and other
machinery is liable to “knock out” the cylinder-heads
or even break the cylinder itself. The cocks C, C,
called cylinder-cocks, are therefore placed in the under
side of the cylinder, so that when they are open if
there is any water in the cylinder it will escape
through the cocks. They are therefore always opened
when the engine is starting, or at any other time when
there is any indication that there is water in the cylinders.
Question 166.How are these cocks opened and
closed?
Answer. A shaft, R R, figs. 92 and 94, which extends
across the frames, has an arm, R S, fig. 92, at
each end. These arms are connected by rods, S T, with
the handles of the cylinder-cocks. The shaft also has
a vertical arm, R U, the upper end of which is connected
by a rod with the cab. At the end of the rod
is a suitable handle, f, fig. 71, by which the cocks can
be either opened or closed at pleasure by the locomotive
runner.
Question 167.How is the piston-rod fastened to the
piston?
Answer. It fits into a straight or tapered hole in the
piston-head, in which it is fastened either with a key,
k k, as shown in figs. 96 and 97,
[44] or by a nut on the
front side of the piston.
[44]Fig. 96
is an end view of the piston with the follower-plate removed.
Fig. 97 is a section through the centre.
Fig. 96.
Fig. 97.
Scale 1¹⁄₂ in. = 1 foot.
Question 168.How is the piston constructed?
Answer. It is made of two cast-iron pieces, B and C,
fig. 97, the one, B, called the piston-head or spider, to
which the piston-rod D is attached. The other part,
C, called the follower-plate, is bolted to the piston-head
by the bolts c, c, called follower-bolts. The piston-head
has lugs or projections, d, d, d, fig. 96, cast
on the inside, to which the follower plate is bolted.
Hollow spaces are thus left between these lugs.
Question 169.How is the piston made to work steam-tight
in the cylinder?
Answer. By means of two rings, A, A, figs. 96 and
97, called packing-rings. These rings are turned of
the same size or a little larger in diameter than the
cylinder. They are then cut open at one point in
their circumference so that they can be pressed apart
or expanded by the springs a, a, called packing springs,
on the inside of the rings. These springs are pressed
out by the nuts and bolts b, b, called packing-bolts and
packing-nuts, so that when the rings wear they can be
expanded so as to fill the cylinder completely. The
place where the one ring is cut is placed opposite that
of the opening in the other ring, or they are made to
break joints, as it is called. This is done to prevent
the steam which leaks through the opening where the
one ring is cut from passing through to the other side
of the piston. These rings are usually made of brass
and have grooves, c, c, fig. 97, turned in them, which
are filled with what is called Babbitt’s metal. This
metal is used because it is less liable to scratch the
cylinders than brass alone. Another ring, l l, made of
cast iron and as wide as the two brass rings, is placed
inside of the latter and is intended to furnish a bearing
for the springs, and thus distribute the pressure of
the springs equally on the packing rings. This iron
ring is also cut open at one point.
Question 170.How is the piston-rod made to work
steam-tight through the cylinder-head?
Answer. By what is called a stuffing-box. This consists
of a cylindrical chamber, r r, fig. 92, which is
made about 1¹⁄₂ inches larger in diameter than the piston-rod.
This leaves a space ³⁄₄ of an inch wide all
around the rod. This space is filled with hemp or
some other fibrous material, called packing, saturated
with oil or melted tallow. This packing is compressed
by a hollow cylinder, s s, called a gland, the inside of
which fits the piston-rod and the outside the stuffing-box.
This gland is forced into the stuffing-box by
nuts, t, t, which are screwed down on a flange, u, attached
to the gland. The packing is thus compressed
in the stuffing-box and forced against the piston-rod,
which is made smooth and perfectly round and
straight, and against the side of the stuffing-box,
so that no steam can escape around the piston-rod.
A brass ring or “bushing” is often put into the
cylinder-head and in the gland where it touches the
piston-rod,[45] because brass will bear the friction of the
rod better than cast iron, and when it is worn out it
can be removed and a new one substituted in its
place.
[45] Locomotive piston-rods are now usually made of steel.
Question 171.Why is the end of the piston-rod
made to work in guides?
Answer. Because it must move in a straight line if
it and the piston work steam-tight in the cylinder.
By referring back to fig. 2, it is obvious that if a
pressure be exerted against the piston B and communicated
to the crank-pin N by the connecting-rod E,
the latter, excepting at the dead-points, will exert a
pressure either upward or downward, according to the
direction the piston is moving. This pressure would
bend the piston-rod if no provision were made to prevent
it. For this reason, therefore, the end of the
piston-rod is attached to what is called a cross-head,
L, figs. 92 and 94, which works in guides, M, M. The
cross-head is made of cast iron and has slides, N, N,
figs. 93 and 94, one on each side, each of which works
between a pair of guide-bars or rods, M, M, shown in
section in fig. 93.[46] These guide-rods, or guides as
they are called, are planed and finished with great accuracy
so as to be straight and smooth, and are attached
to the cylinder-head at one end, and to a support,
O, called the guide-yoke, which is fastened to the
frame at F, fig. 94, and also usually attached to the
boiler. The guides are set with great care, so as to
be exactly parallel with the axis or centre line of the
cylinder, so that the cross-head will slide in exactly
the same path that the piston-rod will if it moves in
a straight line. If then the piston-rod and the connecting-rod
are attached to the cross-head, all the
strain produced by the obliquity of the connecting-rod
will be borne by the guides, thus relieving the
piston-rod, and making it certain that it will move in
a straight line.
Question 172.How are the piston and connecting-rods
attached to the cross-head?
Answer. The end of the piston-rod fits into a tapered
hole in the cross-head and is held by a key, w,
figs. 92 and 94. The connecting-rod is attached to a
pin, Q, called a wrist-pin, which is cast with the cross-head.
Question 173.How is the wear of the slides lessened
and compensated?
Answer. Sometimes they are made with brass
wearing pieces called gibs, shown at N, N, fig. 93,
which are placed between the slides and the guides.
These gibs can either be removed and new ones substituted
when they become very much worn, or by inserting
thin pieces of metal, called liners, between
them and the cross-head, they will be spread apart so
as to fill the space between the slides. The slides are
now, however, oftener made without gibs, and have
recesses either cast or drilled in them, which are filled
with either Babbitt’s metal or glass bearings, which
latter are said to wear very well. The guides are
bolted at each end to blocks, x, x, called guide-blocks,
which can be planed off so as to bring the guides
nearer together when they and the slides are worn.
Sometimes liners are placed between the blocks and
the guides, which can be removed when it is necessary
to bring the guides nearer together.
Question 174.Are the top and bottom guides worn
alike?
Answer. No: the top guide in ordinary engines is
worn the most, because the pressure of the slides is
always on the top guide when the engine is running
forward, and on the bottom guide when it is running
backward. This will be understood by referring back
to the series of figures from 11 to 24. It will be noticed
that in the backward stroke of the piston, represented
by figs. 11 to 17, the strain on the connecting-rod
tends to push the cross-head upward, and in the
forward part of the stroke, figs. 18 to 24, the connecting
rod pulls the cross-head in the same direction. If
the crank turned the opposite way, this action would
be reversed and the cross-head would then be alternately
pushed and pulled downward, and the bottom
guides would then be worn the most. As nearly
all locomotives run forward more than backward, the
top guides are usually worn the most.
Question 175.How are the slides oiled?
Answer. Oil cups, n, o, figs. 92, 93 and 94, are placed
about the middle of the top guide. These cups usually
have a reservoir to hold a supply of oil, and are so
constructed that it will be gradually fed on the slides,
which are thus constantly and regularly lubricated.
Question 176.How are the pumps worked from the
piston-rods?
Answer. The pump-plunger is attached to a projection,
W, figs. 92 and 93, called the pump-lug, cast on
one of the slides of the cross-head. The plunger thus
receives a reciprocating motion from the piston.
Question 177.How are the connecting-rods made?
Answer. They are made of flat bars of wrought iron.
The rods which connect the cross-heads with the
driving-wheels are called main connecting-rods, and
the rods which connect or couple the driving-wheels
together are called coupling-rods.[47]Fig. 98 represents
a side view and a plan of a main connecting-rod. In
the side view the end B, and in the plan both ends of
the rod are shown in section. It is attached to the
wrist-pin at A and to the crank-pin at B. Fig. 99
represents similar views of a coupling-rod. To save
room in the engraving each of these rods is represented
with a part of the middle broken away. The
main rods are usually made wider at G, next the
crank-pin, than at the other end, as it has been found
that they are most liable to break at that end. The
coupling-rods are now made either straight or somewhat
wider in the centre.
[47] They are also often called side or parallel-rods, but the term coupling-rods
is considered the best.
Fig. 98.
Fig. 99.
Scale ³⁄₄ in. = 1 foot.
Question 178.How are these rods prevented from getting
loose on the pins from the wear of the latter in the inside
of the holes of the rods?
Answer. The ends of the rods are provided with
what are called brass-bearings,[48]
or “brasses,” c, d, and
e, f. These brasses are made in pairs, so as to embrace
the pins, from each side. They are held by
⊃-shaped clamps, s s s, called straps, which are
bolted
to the rods. When the brass-bearings become worn,
they are taken out of the straps, and a portion of their
surfaces of contact with each other is filed away, thus
allowing them to come nearer together, and thereby
reducing the size of the hole which receives the pin or
journal. In order to prevent their being loose in the
straps, tapered or wedge-shaped keys, k, k, which bear
against the brasses, are fitted in the straps and rods.
By driving down these keys the brass bearings are
forced together, thus reducing the size of the hole for
the journal, and making the rods fit tightly on the
pins. A hard steel plate, shown by dark shading in
the engraving, is sometimes interposed between the
keys and the brasses to prevent the key from indenting
the surface of the soft brass. As the keys are
very liable to get loose and fall out, they are held
either by screws and nuts, x, x, as shown in the engraving,
or by set-screws on the side of the rods. The
whole arrangement of straps, keys and brasses is called
a stub-end.
[48] The portion of a shaft pin or spindle subjected to friction is called a
journal, and the surface which presses or “bears” against it is called a
bearing.
Question 179.How are the journals of the crank-pins
oiled?
Answer. By oil-cups attached to the straps, above
the journals, similar to the cups used on the guide-rods,
but which are not shown in the engravings of
the connecting-rods. Sometimes oil-cellars, as they
are called, are attached to the under side of the straps.
These are metal boxes, which are filled with oil, which
is agitated violently by the rapid motion of the rods,
and is thus applied to the journals through holes
drilled in the straps. In order to confine the oil and
prevent its leaking out around the journals of the
coupling-rods, the brasses at n, n, fig. 99, are usually
made so as to enclose the outside end of the crank-pin,
which thus not only keeps the oil in, but excludes
the dust. The brasses are usually lined with Babbitt’s
or some other kind of soft metal, which is thought to
be less liable to heat from the friction of the journals.
Question 180.Are the coupling-rods always made
with stub-ends?
Answer. No; their ends are sometimes made in one
piece—that is, without straps or keys. The holes which
receive the crank-pins then have brass rings or bushings,
as they are called, which fit tightly and are
driven into the holes, and form the bearings on the
pins. When these rings become worn they are
driven out and new ones put in.
Question 181.What is meant by the term lost motion?
Answer. It is used to designate the wear of machinery,
which causes a loss of motion in some of the
parts. Thus if the bearings of the main connecting-rods
are worn, the piston must move a distance equal
to the wear at each end of the stroke before it moves
the crank-pin. Lost motion might therefore be called
the looseness of the parts. When we speak of taking
up the lost motion, we mean making parts which were
loose fit tightly.
PART XI. THE VALVE-GEAR.
Question 182.What is meant by the valve-gear of a
locomotive?
Answer. By the valve-gear is meant the arrangement
of eccentrics, rods, links, rockers, etc., by which
the valves are moved and their motion regulated.
Question 183.What is required of the valve-gear in
working a locomotive?
Answer. It must be so arranged that the locomotive
can be run either backward or forward, and so that
the motion of the wheels can be reversed quickly and
with certainty. It should enable the runner to employ
the greatest power of the engine by admitting
steam into the cylinders during the whole or nearly the
whole of the stroke of the pistons, or when less power
is required, to use the steam more economically by
working it expansively, which latter is accomplished
with the present appliances by changing the travel of
the valve.
Question 184.How is the valve-gear constructed so
as to run the engine either backward or forward?
Answer. As already explained, in answer to question
76, two eccentrics are provided for each cylinder.
These are set so that one of each pair will run the locomotive
in one direction, and the other two the reverse
way.
Question 185.How must the eccentrics for each cylinder
be set in order that the one may run the engine forward
and the other backward?
Answer. This can be best explained by reference
to fig. 100, in which the piston, P, is represented
at the beginning of the backward stroke, and the
valve V has the requisite lead and is just about to
open the front steam-port. It is obvious that, in
order to complete the backward stroke of the piston,
the front port must be opened to admit steam
into the front end of the cylinder, and therefore the
valve must be moved in the direction indicated by the
dart a. To do this, the upper arm of the rocker r must
move in the same direction, and the lower arm must be
moved the reverse way, as indicated by the dart e. If
the crank is intended to move in the direction indicated
by the dart N, then the centre of the eccentric
must be above the centre of the shaft or axle, in order
to move the rocker in the direction indicated by the
dart e. Supposing, however, it was intended to move
the crank the reverse direction, as shown by the dart
N in fig. 101; it is evident in that case that the valve
must be moved in the same direction as before, in
order to open the front steam-port and thus admit
steam to force the piston back. But if the crank
turns in the direction shown by the dart N, fig. 101,
then the centre of the eccentric must be placed below
the centre of the axle in order to move the lower
rocker arm in the direction of the dart e and the valve
in that indicated by a. It will thus be seen that the
centres of the eccentric for running forward and that
of the one for running backward must be placed, the
one above and the other below the centre of the axle
at the beginning of the stroke of the piston, as shown
in figure 101.
Fig. 100.
Fig. 101.
Fig. 102.
Scale ³⁄₈ in. = 1 foot.
Question 186.Why is it that the centres of the eccentrics
are not placed opposite to each other on the axle?
Answer. Because before the beginning of the stroke
of the piston it is necessary to move the valve from
its middle position a distance equal to the lap before
the steam-port begins to open. If we have a valve
like that shown in fig. 10—that is, without any
lap—the centres of the eccentrics could be placed at
right angles, or, as mechanics say, “square” with the
crank, as was shown in fig. 11, and exactly opposite
to each other, because such a valve begins to take
steam as soon as it moves from the middle of the
valve-face. If, however, we have a valve like that
shown in fig. 27, it is plain that before it will admit
or take steam, as it is called, in either of the steam-ports,
it must be moved from the centre of the valve-face,
or its middle position, a distance equal to the lap,
L. For this reason, therefore, the eccentric, instead
of being placed at half-throw,[49] as it is called, must be
so far ahead of the middle position as to have moved
the valve a distance equal to the lap, and if any lead
is given to the valve, equal to the lap and lead together.
In figs. 100 and 101, f g is a vertical line at
right angles to the crank at the beginning of the
stroke. It will be seen that the centre of each of the
eccentrics is set far enough ahead of this line to give
the valve the required lead. When the piston reaches
the back end of the cylinder, the two eccentrics will
occupy the position shown in fig. 102, in which position
the lower one would move the valve so as to turn
the crank in the direction of the dart N, and the
upper one in the reverse direction. It will be seen
that in this position both of the eccentrics are again
ahead of half-throw, when the piston is at that end of
its stroke.
[49] This would be at right angles to the crank when the piston is at the
end of the stroke.
Fig. 103.
Scale ³⁄₄ in. = 1 foot.
Question 187.How is the motion of either eccentric
communicated to the valve?
Answer. The ends of each pair of eccentric-rods
are connected together by a link, a b, fig. 103. This
link has a curved groove or slot, a b, in it, in which a
block, B, fits accurately, so that it can slide freely
from one end to the other. This block is attached to
the lower rocker-arm by a pin, c, which works freely
in the block. The two eccentric-rods C and D are
attached to the ends of the link at e and f by pins and
knuckle-joints. It is apparent that if the link is
down, or in the position shown in fig. 103 and also on
a smaller scale in fig. 104, the motion of the upper
eccentric-rod, which is usually used for the forward
motion, will be imparted to the rocker, and thus to
the valve, and when the link is in the position shown
in fig. 105, that the valve will be moved by the lower
or backward eccentric-rod B. In order to reverse the
engine, it is then only necessary to provide the means
of raising and lowering the links. This is done by a
shaft, A, fig. 103, called a lifting-shaft, which has two
horizontal arms, E,[50] one for each link, and a vertical
arm, F. The links are suspended from the ends of
the horizontal arms by rods or bars, g h, called link-hangers,
which are connected to the links and to the
arms above by pins, which enable the hangers to vibrate
freely. The lower pin is attached to a plate,
L d, called a link-saddle, which is bolted to the link.
The vertical arm of the lifting-shaft is connected by
a rod, G G, called the reverse-rod, to a lever O, O,
Plate II. in the cab called a reverse-lever, the construction
of which will be explained hereafter. This lever
is worked by the locomotive runner, and by moving
the upper end of it forward, the link will be lowered,
and the rocker and valve will be moved by the forward
eccentric; and if the reverse-lever is moved back, the
link will be raised, and the backward eccentric will
move the valve. When this is done, the valve-gear is
said to be thrown into the forward or backward motion,
or forward or back gear.
Question 188.How is the travel of the valve changed
by the motion of the link?
Answer. By either raising or lowering the link, so
that the link-block and rocker-pin will be some distance
above or below the eccentric-rods. Thus in fig.
104, the motion of the upper eccentric-rod, and in fig.
105 that of the lower or back eccentric-rod is communicated
to the rocker-pin and the valve. If, however,
the link should be raised so that the link-block and
rocker-pin are somewhat below the upper or forward
eccentric-rod, as shown in fig. 106, then the motion
imparted to the rocker and valve will partake somewhat
of that of the upper and also of the lower eccentric-rod.
So long as the rocker-pin is above the
centre of the link, the motion of the valve will partake
most of that of the upper or forward rod, and the engine
will then run forward, but when the rocker-pin
is below the centre of the link, its motion will be influenced
more by the back eccentric-rod, and the engine
will then run backward.
The motion of the link, which is somewhat complex
and difficult to understand clearly, will perhaps be understood
better if we represent it in a number of successive
positions of the whole stroke of the piston, as
was done to show the motion of the eccentric in figs.
11 to 24. We will therefore suppose that the link is
in what is called full gear forward, as shown in figs.
103 and 104. In fig. 108 the link is in the position
it would occupy at the beginning of the stroke of the
piston; in fig. 109 it is in that which it will be in
when the piston has moved four inches; in fig. 110,
when it has moved eight inches; in fig. 111, twelve;
and in figs. 112, 113 and 114, sixteen, twenty and
twenty-four inches. Figs. 114 to 119 represent the
successive positions of the link during the return
stroke. In order to show the different positions of
the link we have represented on a larger scale, in fig.
120, the successive positions of the centre line of the
link, which will indicate the motion imparted by it to
the rocker. In order to designate each of these positions,
the centre lines in fig. 120 are numbered + and
-0, 4, 8, etc., etc., to correspond with similar numbers
in figs. 108 to 119.
Fig. 108.
Fig. 109.
Fig. 110.
Fig. 111.
Fig. 112.
Fig. 113.
Fig. 119.
Fig. 118.
Fig. 117.
Fig. 116.
Fig. 115.
Fig. 114.
Scale ³⁄₈ in. = 1 foot.
Fig. 120.
Scale ³⁄₁₆ in. = 1 inch.
Fig. 121.
Scale ³⁄₁₆ in. = 1 inch.
Fig. 122.
Scale ³⁄₁₆ in. = 1 inch.
Thus the line -0 -0 represents the position of the
centre of the link which it occupies at the beginning of
the stroke as shown in fig. 108. The line -4 -4, that
represented by fig. 109, when the piston has moved
4 in. The lines -8 -8, -12 -12, -16 -16, -20 -20, 24
24, +4 +4, etc., the successive positions of the centre
of the link represented in figs. 108 to 119. The dotted
lines h a and h b represent the two extreme positions
into which the rocker-arm would be moved by
the action of the link. It will be seen that when the
link is in the position shown, it imparts the full stroke
of the eccentrics to the rocker-pin and consequently
to the valve. We will now suppose that the link is
raised up as shown in fig. 106, so that the position of
the rocker-pin is just half-way between the end of the
eccentric-rod and the centre of the link. This position
is called half-gear. In fig. 121 the different
positions of the centre line of the link and of the
rocker have been laid out for half-gear in the same
way as was done for full-gear before. From this it
will be seen that the travel, a b, imparted to the rocker-pin
and valve by the link when it is in the position
shown, instead of being 5 in. is only 3¹⁄₂ in. In fig.
107 the link is raised up, so that the rocker-pin is in
the centre of it or midway between the eccentrics.
This position is called mid-gear. The successive positions
of the centre line of the link in this position
have been laid down in fig. 122 in the same way as
was done for full and half-gear. The movement of
the rocker, it will be seen, is, for mid-gear, only 2¹⁄₂ in.
These diagrams show that when the rocker-pin is opposite
the eccentric-rod, the valve receives the full
throw of the eccentric, and that the motion imparted
by the eccentric diminishes as the rocker-pin approaches
the centre of the link, so that, with eccentrics
having 5 in. throw and a valve with ⁷⁄₈ lap and ¹⁄₈
in. lead, we can increase or diminish the travel of the
valve from 2¹⁄₂ to 5 in. by simply raising or lowering
the link, which is done by the reverse-lever.
Question 189.What is the effect of this variation of
travel on the working of the valve and the admission and
release of steam to and from the cylinder?
Answer. It is almost precisely the same as that
which is effected by increasing or diminishing the
throw of the eccentric, which was explained in the
answer to Question 52. In order to show this effect
more clearly, we have represented by motion-curves,[51]fig. 123, the movement imparted to the valve by the
link when it is in full, half and mid-gear, as illustrated
in the preceding figures. The curve for full-gear
is engraved in full heavy lines; that for half-gear
in lighter lines, and for mid-gear in dotted lines.
From these curves it will be seen that when the valve
is worked in full-gear the steam-port is opened wide
at 2 in. of the stroke and steam cut off at 21 inches.
When the valve is worked in half-gear the port is not
at any time opened wide and steam is then cut off at
17¹⁄₂ in. of the stroke, and when worked in mid-gear
the greatest opening of the steam-port is no greater
than the lead and the cut-off occurs at 4 inches of the
stroke.
[51] The nature of these curves was explained in answer to Question 44.
It is of course possible to work the link in any intermediate
position between those which we have represented.
Usually the reverse-lever is arranged so
that the steam will be cut off at 6, 8, 10, 12, 15, 18,
and 20 inches of the stroke.
Question 190.What is the greatest and the least
admission of steam possible with the ordinary link motion?
Answer. With 24 in. stroke of piston and 5 in. travel
and ⁷⁄₈ in. lap, steam can be admitted as shown by the motion-curves
during 21 in. or 87¹⁄₂ per cent. of the stroke,
and can be cut off at about 4 in. or 16²⁄₃ per cent. It
will be seen, however, that in mid-gear the motion-curve
becomes a straight line, and that the pre-admission
of steam, that is the admission of steam before the
piston reaches the end of the stroke, is equal to that
admitted after, so that it is impossible to work the locomotive
with the link in that position. Practically
it is found that no useful work can be done with a
link if the steam is cut off at less than six inches, or
one-fourth of the stroke. Even then the opening of
the steam-ports is so small that the steam which enters
the cylinders is very much wire-drawn.
Question 191.How are the curves drawn which represent
the motion of the valve?
Answer. These motion-curves as produced by the link-motion
are very difficult to draw, as the motion of the
link is extremely complicated. It is doubtful, therefore,
whether those who have no knowledge of mechanical
drawing will be able to understand the following
description of the method of doing it, which
we will try to make as clear as possible.
Fig. 123.
Scale ³⁄₁₆ in. = 1 inch.
Fig. 124.
Scale ³⁄₄ in. = 1 foot.
In the first place, the centre S, fig. 124, of the axle,
A, of the rocker, and B of the lifting-shaft, must be
laid down in their proper positions. If, now, the valve
has ⁷⁄₈ in. lap and ¹⁄₈ lead, the lower rocker-pin must be
one inch ahead of its middle position when the piston
is at the front end of the cylinder, and at the beginning
of the backward stroke. We will, therefore,
mark the centre, a, of the rocker-pin in this position.
If from the centre of the axle a circle, c d e, be drawn
whose diameter is equal to the throw of the eccentrics,
this circle will represent the path in which the centres
of the eccentrics will revolve. If, now, the distance
from the centre of the axle to the centre of the
lower rocker-pin, a, when the latter is in its middle
position, be taken for a radius,[52] and from the position
of the rocker-pin at the beginning of the stroke as a
centre, the circle representing the path of the eccentrics
be intersected at two points, c and d, the
points of intersection will represent the positions
of the centres of the forward and backward eccentrics.
Having determined these positions, draw
arcs of circles, f and g, from these centres with a radius
equal to the distance from the centres of the eccentrics
to the centres of the pins which connect the
rods to the link. It is evident that at the beginning
of the stroke the centres of the pins in the link must
each be in one of these arcs. But the link is suspended
by the hanger, i h, which oscillates from the
end, i, of the lifting-arm, which for any one point of
cut-off is stationary; and therefore the point of suspension
of the link must always be in the arc, j k, described
from the centre of the pin, i, in the lifting-arm,
with a radius equal to the length of the hanger.
There are, therefore, three points in the link, each of
which must be in one of the arcs which have been
drawn, and which will determine the position of the
link. This can be done easiest by drawing the link,
L, fig. 125, on a stiff piece of paper, m n, and cutting
off the back, p q, of it through the centres of the pins,
s and t, and also cutting out a triangular piece, u, the
apex of which will correspond with the centre of the
point of suspension, o. By placing this piece of paper
on the drawing it can be moved, so that the three
centre points, s, t and o, will respectively conform with
the arcs, f g and j k, fig. 124. In this position the
piece of paper will then be in the position of the link
for the point of the stroke represented. By marking
the centres of the link-pins on the arcs f and g, and
from them as centres, with the length of the rods used
to draw the arcs, two other arcs, v, w, be drawn intersecting
each other, the point d, where they intersect
will be the centre from which the centre line of the
link can be drawn with a radius, l d, equal to the distance
from the centre of the eccentrics to the centre of
the link. This will give the first position -o -o, of
the centre line of the link. As the rocker-pin must
always be in the centre of the link, it is obvious that
the point at which the centre-line of the link intersects
the arc in which the rocker-pin oscillates must
be the position of the centre of the rocker-pin. With
this determined the position of the valve can easily be
located.
[52] This is usually the radius of the link but in some cases either a
longer or shorter radius is taken to draw the link. In the following explanation
it is assumed that the link is drawn with this radius, or from
the centre of the axle. Of course if a greater or lesser radius is used, due
allowance must be made therefor.
Fig. 125.
Scale, ³⁄₄ in. = 1 foot.
In order to represent the link at any other point of
the stroke, say after the piston has moved four inches,
the position of the crank must first be laid down. To
do this, allowance must be made for the irregularity
due to the angularity of the connecting-rod, which
was explained in answer to Question 54. From the
centre of the axle, a circle, C D, whose diameter is
equal to the stroke of the piston, is first drawn, which
will represent the path of the crank-pin. A horizontal
centre line, E F, should also be drawn through the
centre of the axle and the centre of the cylinder.
The intersection o of this line with the path of the
crank-pin will be the position of the latter at the beginning
of the stroke. If from this point a distance,
o o, be laid off on the centre line equal to the length
of the connecting-rod,[53] it will give the position of the
wrist-pin at the beginning of the stroke, so that from
this its successive positions for each inch of the stroke
can be laid off. From its position after the piston has
made say four inches of the stroke as a centre, and
the length of the connecting-rod as a radius, if the
path of the crank-pin be intersected at -4, the point
of intersection will represent the position of the crank-pin
at four inches of the stroke. The distance from
o to -4 is equal to 44 degrees of the whole circle.
The eccentrics, being attached to the axle, of course
move the same number of degrees that the crank does,
and therefore, in order to determine their position
when the crank has moved any distance, it is only necessary
to move them as many degrees as the crank
has. This can be done very easily by extending the
radii of the eccentrics, when they are in the first position,
until they intersect the path of the crank-pin at
c′ and d′. By stepping off from the latter points of
intersection a distance c′ c‴ and d′ d‴, equal to o -4,
which the crank has moved, and then drawing other
radii from the two points c‴, d‴, their intersection,
c″ d″, with the path of the eccentrics will represent
the position of the centres of the eccentrics when the
crank is at -4. Having determined the position of
the eccentrics, the link can be laid down as before,
that is, from c″ and d″ as centres and with the length
of the eccentric-rods as a radius arcs, f″ and g″, are
drawn. Then with the paper template the positions
of the centres of the link-pins in these arcs are determined
and marked, and from them with the length of
the eccentric rods as a radius, two intersecting arcs,
v″, w″, are drawn, whose intersection gives the centre
of the link from which its centre line, -4 -4, is
drawn. This will give the position of the rocker-pin
for another point of the stroke. In a similar manner
its position can be determined for any number of
points of the stroke, from which the position of the
valve can easily be determined and laid down on the
diagram for the motion-curve as was described in the
answer to Question 44. Of course the valve will be
moved from its middle position the same distance that
the rocker-pin is,[54] only in an opposite direction. In
order to lay down the position of the valve on the
diagram for motion-curves, it is, therefore, only necessary
to draw it in the same relative position as that of
the rocker-pin which is given by the point of intersection
of the center line of the link with the path in
which the rocker-pin oscillates. To construct the
motion-curves it is necessary to determine the positions
of the valve for different points of the stroke
and mark them on the horizontal lines which represent
the respective positions of the piston. Curves
are then drawn through these points, either by hand
or by constructing templates. The more points there
are determined, the more accurate will be the curves.
It is, therefore, best to lay down the position of the
valve for each inch of the stroke of the piston. They
should also be drawn full size, which of course was
impossible for the illustrations which are given herewith.
[53] In order to get the engraving within the required limits, the diagram
is drawn with a connecting-rod only 5¹⁄₂ instead of 7 feet. The latter is
the length used in previous illustrations.
[54] This will be the case when the two arms of the rocker are of the
same length, as they usually are. Sometimes, though rarely, they are
of different lengths.
Question 192.Is there any other method of drawing
these motion curves?
Answer. Yes: models which show the working of
the valve-gear have been constructed with a pencil, to
which the reciprocating motion of the valve is imparted,
and which traces a curve on a surface having
the same motion as the piston. This method has
been employed by the writer in an instrument which
he has applied to the locomotive itself. The principle
upon which it works will be understood by supposing
that the steam and exhaust-ports as represented in the
diagram for motion-curves, fig. 123, be drawn on a
board, A B C D, fig. 126, but instead of standing vertical,
as in fig. 123, they are represented in a horizontal
position, and the board on which they are drawn
is fastened to the cross-head, L, so that the former will
move backward and forward simultaneously with the
latter and the piston. A small shaft, F, is attached to
suitable supports, j, which are fastened to the guides.
This shaft has two arms, G and E, one vertical and the
other horizontal and of the same length. The upper
end of the vertical one, G, is then attached to the valve-stem
or rocker-arm by a short connecting-rod, H, or
other suitable means, so that the movement of the
valve-stem will be imparted to the arm and shaft.
Of course the end of the horizontal shaft then has exactly
the same motion vertically that the valve-stem
and valve have horizontally, with the very trifling inaccuracy
due to the fact that the movement of the one
is in a straight line, whereas the other is in the arc
of a circle.
Now if a pencil, P, is attached to the end of the
horizontal arm, E, and is set so that its point indicates
the exact position of the steam edge, h, of the valve,
as shown in fig. 123, it is obvious that when the piston
and board have moved four inches, the pencil will have
moved downward and have drawn the portion of the
motion-curve from h to i; and when the piston has
moved eight inches the curve will be drawn to j, and
at 12, 16, 20 and 24 inches of the stroke the curve
will be drawn to k, l, m and n. During the return
stroke a corresponding curve, n o h, will, of course, be
drawn. With such an instrument curves can be
drawn for any position of the link, and they will show
the exact movement of the valve during the whole
stroke, and will indicate all the defects resulting from
bad proportions or construction, lost motion in the
parts, or other causes of error or irregularity.
Fig. 126.—Scale ³⁄₄ in. = 1 foot.
In using this instrument, however, it is impracticable
to attach a board to the inside of the cross-head,
and it must therefore be fastened to the outside. The
horizontal arm E should be made of thin steel, so as to
form a spring. The end has a small boss[55] with a hole
in it ³⁄₁₆ of an inch in diameter. This hole has a
screw thread cut in it, into which an ordinary hard
drawing pencil is screwed. The spring is so arranged
that the pencil will not be in contact with the board
unless it be pressed against it. The locomotive is
then placed on a smooth piece of track with steam on
and run very slowly, so that a person walking alongside
can press the pencil against the surface of the
board, which should be covered with drawing paper.
By watching the cross-head when it reaches the end
of the stroke, the pencil can then be pressed against
the paper and kept in contact through the whole
stroke and instantly released when the motion-curve
is completed. The link can then be placed in another
position, and thus any number of curves can be drawn,
which will furnish the most accurate means of analyzing
the motion of the valve.
[55] The term “boss” is used to imply an enlargement or increased
thickness of any part.
In practice it is best not to draw the lines which
represent the edges of the ports, until after the curves
are drawn and the paper removed from the board. A
centre line must, however, be drawn on the engine from
which to lay off the ports. This can be done by placing
the valve in its middle position, and then fastening
the shaft F in that position with a nut which should
be provided for that purpose on the end of the shaft.
After it is fastened in this position, detach the connecting-rod
H, and with one stroke of the piston a
centre line can be drawn with the pencil P. From
this centre line the edges of the ports can easily be
laid off and drawn on the paper after it is taken off
the engine.
Question 193.Can the position of each edge of the
valve, with any given amount of travel, be shown in its
relation to the ports by one motion-curve, or is it necessary
to draw such curves for each edge of the valve, as shown
in fig. 28?
Answer. One motion-curve is sufficient to represent
the position of any part of the valve during the entire
stroke. This will be apparent if it is remembered
that each motion-curve is exactly like the others, as
shown in fig. 28, the only difference being that the
ports occupy different positions in relation to the
curves. It is, therefore, only necessary to draw lines
to represent the relative positions of the ports to the
other curves to show the entire motion of the valve by
one curve. To illustrate this it will be assumed that
a motion-curve, h i j k l m n o p, and a centre line, a
b, fig. 127, have been drawn with the instrument described
in the answer to the previous question. The
centre line a b, which will be equal in length to the
stroke of the piston, should then be divided into
inches, and lines ff, 23 1, 22 2, etc., should be drawn
through the points of division and at right angles to
a b. If, now, we want to show the movement of the
front steam edge of the valve in relation to the corresponding
steam port, a line, t, should be drawn perpendicular
to f f, to represent that edge of the valve
at the beginning of the stroke. As it is impossible to
determine accurately the position of this steam edge
at the beginning of the stroke from the motion-curve,
which is then tangent[56] to the line f f, we must lay it
off from the centre line, a b. This can readily be
done if we remember that if a valve has ⁷⁄₈ in. lap
when it is in the middle position, as shown in fig. 27,
and ¹⁄₁₆ in. lead at the beginning of the stroke, it must
have moved ¹⁵⁄₁₆ in. from the middle position at the beginning
of the stroke as shown in fig. 28. The line
t must therefore be drawn ¹⁵⁄₁₆ in. from a b to represent
its proper position in relation to the motion-curve, and
as it has ¹⁄₁₆ in. lead, the steam edge, h h′, of the steam-port
must be drawn at that distance from t. Another
line, m m′, can then be drawn to represent the width
of the front steam-port, c c′. From these lines the
movement of the valve in relation to the front port,
c c′, and the admission of steam are shown as clearly
as in fig. 28.
[56] A curve is said to be tangent to another carve or to a straight line
when the two just touch, but do not intersect or cross each other.
If now we want to represent the motion and relative
position of the back steam edge of the valve in
relation to its port, it is only necessary to assume that
the line t represents that edge, and that the curve h i
j k l m n o h represents its motion, and to draw the
back steam-port in its proper relation to it. When
the valve is in its middle position, as shown in fig. 27,
the outside edge of the port h is ⁷⁄₈ in., or a distance
equal to the lap, from the steam edge q of the valve.
As the center line a b, fig. 127, represents the middle
position of the edge of the valve, it is only necessary
to draw a line, n n′, ⁷⁄₈ in., or the same distance from
the centre line a b that the outer edge of the port d is
from q in fig. 28, to represent this edge of the port in
fig. 127, and another b b′, at a distance from the former
equal to the width of the port, to represent its
inner edge. A line, q, below the line 0 24, will represent
the edge of the valve at the beginning of the forward
stroke. The curves in relation to the port d will
then show the motion of the valve in relation to this
port, in the same way that the dotted curve d f does
in fig. 28.
Fig. 127.
Scale ³⁄₁₆ inch = 1 inch.
If it is desired to represent the motion of the exhaust
edge h′, fig. 28, of the valve, it is only necessary
to imagine that the line t, fig. 127, represents that
edge, and then draw in the port d in the same relation
to it that it bears to the edge h′, in fig. 28. This
has been done in dotted lines, c c′ and e e′, in fig. 127.
If the reader will cut a paper section of a valve like
that shown in fig. 27 and place the different edges, h,
i, h′ and q, so that they will successively correspond
with the line t in fig. 127, the diagram will perhaps
be more clear. If, for example, the paper section
be placed to the right of the line t, so that the
edge h will correspond with t, then it will be seen that
the port c occupies the same relation to it that it does
in fig. 28. If the valve be placed to the left, so that
the edge q corresponds with t, then the port d will be
in the same relation to it that it has in fig. 28. If
the edges i and h′ be made to correspond with t, then
the ports drawn in dotted lines in fig. 127 will represent
the ports c and d in fig. 28.
The position of the ports in relation to the centre
line of the motion-curve can be determined, if it is
kept in mind that the centre line a b, fig. 127, represents
the position of the different edges of the valve
when the latter is in the middle of the valve-face as
shown in fig. 27, and that the ports must be on the
same side, and the same distance from the centre line
that they are from the edge of the valve whose motion
is represented. Thus if the movement of the steam
edge h in relation to its port, c, was represented, the
edge of the latter must be drawn on the motion diagram
the same distance from the centre line that it is
from h when the valve is in its middle position as
shown in fig. 27. This distance is of course just equal
to the lap of the valve. If the motion of the exhaust
edge h′ was represented in relation to the steam port
d, then the inside edge of the latter would be drawn
the same distance from the centre line a b in the diagram
that the inner edge of the port is from the edge
h′ of the valve, which is equal to the inside lap. The
exhaust port could also be drawn in the same way, but
it would be liable to confuse a diagram made to so
small a scale as that which has been employed for the
accompanying illustrations, and it has therefore been
omitted. Diagrams of this kind which are made full
size will, of course, show the movement of the valve
more distinctly than is possible in the space occupied
by the illustrations herewith. When they are made
of full size, the lines indicating the ports should be
drawn of different colors, so as to distinguish them
from each other easily. Such diagrams will show the
position of the valve in relation to the ports, and indicate
the distribution of the steam during the whole
stroke. It is only necessary to refer the curve to
the proper line to determine the position of the valve
in relation to either of the ports for either the admission
or release of the steam. If, for example, we want
to observe how the admission of steam is governed
by the valve, by referring to fig. 127 we see that at
the beginning of the backward stroke the valve has
¹⁄₁₆ inch lead; that at 1³⁄₄ inches of the stroke the port
c is wide open, as shown by the intersection of the
motion-curve with the line m m′; that the valve has
received its maximum backward travel at 9 inches of
the stroke, and begins to close the port at 15¹⁄₂ inches,
and completely closes it at 21 inches of the stroke.
By referring the motion-curve to the lines n n′ and b b′,
we see that the valve as shown by the line q at n′
again has ¹⁄₁₆ inch lead at the beginning of the forward
stroke; that the steam port is wide open at 1³⁄₈ inches
of the stroke; begins to close at 16¹⁄₄ inches, and is
completely closed at 21 inches. By referring the
curve to the lines e e′ and c c′ we see that the front port
begins to open to the exhaust before the piston has
completed its forward stroke and when it has nearly
an inch to move, that it is wide open almost immediately
after the piston begins its stroke, does not begin
to close until the piston has moved 19¹⁄₂ inches of its
stroke, and is completely closed at 23 inches of the stroke.
By referring the curve to the lines d d′ and g g′, almost
the same phenomena will be observed for the forward
stroke. In fact from such a diagram the whole motion of
the valve can be studied and analyzed with the greatest
accuracy; and, as has already been shown, the
motion imparted to a slide valve by a link is of so
complicated a nature that it is almost or quite impossible
to observe its exact nature without such diagrams.
Question 194.Can a motion diagram be constructed
to represent the motion of the valve with different amounts
of travel?
Answer. Yes; it is only necessary to construct motion-curves
for the same diagram for each distance
traveled, and they will show the movement of the
valve for the given amount of travel represented by
the curves. This has been done in fig. 128, which is
a reduced copy of a series of motion-curves taken from
a locomotive. From this diagram the movement of a
slide-valve worked by the link-motion can be seen
from the highest to the lowest practicable point of cut-off.
For convenience of reference the curves have been
numbered.
Fig. 128.
Scale ³⁄₁₆ inch = 1 inch.
The smallest travel of the valve represented by
curve No. 1 is a little less than 2¹⁄₂ in., and the ports
are then opened only about ⁵⁄₁₆ in., and the steam is
cut off at 8 in. on the backward and 6³⁄₄ in. on the
forward stroke. The exhaust is opened or the steam
is released during the backward stroke at 17 in., and
during the forward stroke at 16⁵⁄₈. When the valve
works with its greatest travel, as represented by curve
8, it travels 5 in., and opens the steam port wide at 3
in. of the backward stroke and 2¹⁄₄ in. of the forward
stroke. The steam is cut off at 20³⁄₄ and 20¹⁄₂ in., and
its release takes place at 23¹⁄₈ in. of each stroke. The
following table gives the greatest width of opening,
the point of cut-off, the point of release, and the lead
for each motion-curve on the diagram. This table
has been made up from the motion-curves drawn with
the instrument described in answer to Question 191,
on a locomotive which had been running about eighteen
months and whose valve-gear consequently was considerably
worn, as s indicated by the flatness of the
motion-curves on each side at the point when the motion
of the valve was reversed. This flatness was
caused by the lost motion in the valve-gear, the pencil
remaining for a time stationary when the motion was
reversed and while the parts were moving from their
bearings on one side to those on the other. The
curves and the table therefore show the operation not
of a theoretically perfect valve-gear, but are examples
of actual practice, with such imperfections as are incidental
to ordinary locomotives. It will be seen that
the instrument shows not only what the valve-gear
should, but what it actually does do, and delineates
all its imperfections.
No. of curve.
Travel of valve.
Width of opening of steam-port.
Point of cut-off.
Point of release.
Lead.
Backwd stroke.
Forw’rd stroke.
Backwd stroke.
Forw’rd stroke.
Backwd stroke.
Forw’rd stroke.
in.
in.
in.
in.
in.
in.
in.
in.
1
2
¹⁄₂
¹¹⁄₃₂
⁵⁄₁₆
8
6
³⁄₄
17
16
⁵⁄₈
⁹⁄₃₂
2
2
⁵⁄₈
⁷⁄₁₆
¹³⁄₃₂
9
¹⁄₂
9
¹⁄₂
18
⁵⁄₈
18
⁵⁄₁₆
¹⁄₄
3
2
⁷⁄₈
⁹⁄₁₆
¹⁄₂
12
11
³⁄₄
19
³⁄₄
19
⁹⁄₁₆
⁷⁄₃₂
4
3
¹⁄₈
¹¹⁄₁₆
⁴¹⁄₆₄
14
14
20
¹¹⁄₁₆
20
⁹⁄₁₆
³⁄₁₆
5
3
¹⁄₂
⁷⁄₈
²⁷⁄₃₂
16
¹⁄₂
16
¹⁄₂
21
¹¹⁄₁₆
21
¹⁄₂
⁵⁄₃₂
6
4
1
¹⁄₈
1
³⁄₃₂
18
¹⁄₄
18
¹⁄₈
22
³⁄₈
22
¹⁄₄
¹⁄₈
7
4
¹⁄₂
1
¹⁄₄
1
¹⁄₄
19
⁵⁄₈
19
¹⁄₂
22
¹³⁄₁₆
22
³⁄₄
³⁄₃₂
8
5
1
¹⁄₄
1
¹⁄₄
20
⁵⁄₈
20
¹⁄₂
23
¹⁄₈
23
¹⁄₈
¹⁄₁₆
Question 195.What are the chief dimensions of the
valve-gear represented in fig. 128?
Answer. The throw of eccentrics was 5 in., the steam-ports
were 1¹⁄₄ in., and the exhaust-port 2³⁄₄ in. wide,
the valve had ⁷⁄₈ in. outside and ¹⁄₁₆ inside lap and ¹⁄₁₆ in.
lead at full stroke.
Question 196.What relation is there between the
distance which the ports are opened by the valve, and its
travel when worked by a link?
Answer. As explained in the answer to Question 52,
the width which the steam-ports are opened by the
valve for the admission of steam diminishes with the
travel of the valve. This is shown very clearly by
the motion-curves, and also in the above table, from
both of which it will be seen that when the valve
travels only 2¹⁄₂ in. the steam-ports are opened only
¹¹⁄₃₂ in. for the back stroke and ⁵⁄₁₆ for the front.
With 2⁵⁄₈ travel the opening is ⁷⁄₁₆ and ¹³⁄₃₂ in. With
4 in. travel the port is opened 1¹⁄₈ and 1³⁄₃₂ in. and
with 4¹⁄₄ in. travel they would be opened wide.
With 4¹⁄₂ and 5 in. travel, as will be seen from the
motion diagram, the ports are not only opened wide,
but the valve throws “over” them, or travels beyond
their inner edges.
Question 197.How is the point of cut-off affected
by the link?
Answer. Changing the travel of a valve with a link
has a very similar effect to that produced by eccentrics
of different throw—that is, the period of admission is
increased with the throw of the eccentric and that for
expansion lessened. This is shown clearly in both
the motion diagram and the table. With the first
curve and a travel of 2¹⁄₂ in. the steam is cut off at 8
in. for the backward stroke and 6³⁄₄ in. for the front,
and with 5 in. travel steam is admitted during 20⁵⁄₈ in.
of the backward and 20¹⁄₂ in. of the forward stroke.
Question 198.How is the point of release or exhaust
of the steam affected by the link?
Answer. As the travel increases, it is delayed until
later in the stroke. Thus, with 2¹⁄₂ in. travel the
steam is exhausted or released from the cylinder
during the backward stroke when the piston has
moved 17 in., and on the return stroke at 16⁵⁄₈ in.,
whereas, with 5 in. travel of the valve, the release is
delayed until 23¹⁄₈ in. of the stroke. An examination
of the diagram and table will show very clearly the
relation of the point of release to the travel.
Question 199.How is the lead affected by the ordinary
link motion?
Answer. It is increased as the travel is diminished,
as is shown in the table, and also by the inclination
of the curves at the top and bottom of the diagram.
Fig. 129.
Fig. 130.
Fig. 131.
Scale ³⁄₄ in. = 1 foot.
Question 200.What is the cause of this change of
the amount of lead?
Answer. This can be best explained by reference to
fig. 129, which represents a link with very short eccentric
rods. If now the centre from which the link was
drawn was in the centre of the axle S, and the eccentric
straps embraced the axle instead of the eccentrics,
their ends c and d would each describe the same arc,
a b, parallel with the centre line, x y, of the link, and
the latter could then obviously be raised and lowered
without moving the rocker-pin at all. But the eccentric
straps being attached to the eccentrics, as shown
by the dotted lines, when the rods are raised or
lowered they describe arcs, c e and g h, from the centres
s and t of the eccentrics, and not from the centre
of the axle. When the link is raised then, the end
of the upper rod obviously moves in the arc c e, and
the top of the link is moved from the axle, as shown
in fig. 130, a distance equal to the interval between
the arc, a b, drawn from the centre of the axle, and
e f, which the rod describes from the centre of its
eccentric. When the link is lowered from back to
mid-gear, a similar action takes place, as the end, d,
fig. 130, of the lower rod describes an arc, f g, so that
the whole link is thrown from the axle a distance
equal to the space between the arcs described from the
centre of the axle and the centres of the eccentrics.
When the position of the eccentrics is reversed, as
shown in fig. 131, the link is moved towards the axle,
thus causing an increase of lead on the opposite side
of the valve. We have employed for our illustrations
very short eccentric rods, in order to make this action
apparent by exaggerating it. It is obvious from the
engravings that the difference in the lead is increased
as the eccentric rods are shortened, and also as the
distance between the points of connection of the rods
with the link is increased. It will also be plain that
increasing the throw of the eccentrics, that is, increasing
the distance of the centres s, s, of the eccentrics
from the centre S of the axle will also increase the
variation in the lead in full and mid-gear.
Question 201.What is meant by the distribution of
steam in the cylinder?
Answer. It means the admission and exhaust of
steam to and from the cylinder in relation to the
stroke of the piston or the revolution of the crank.
Question 202.What are the principal periods or elements
of the distribution of steam by the slide-valve and
link motion?
Answer. They are:
1. The pre-admission or lead, that is, the admission
of steam into the cylinders in front of the piston before
it has completed its stroke.
2. The admission of steam after the piston has commenced
its stroke.
3. The expansion of steam in the cylinder.
4. The pre-release, or exhaust of steam before the
piston has completed its stroke.
5. The release, or exhaust during the return stroke
of the piston.
6. The compression of steam, or closing the exhaust
before the piston has completed its return stroke.
Question 203.What is meant by the clearance of the
piston?
Answer. It is the space between the piston and the
cylinder-head when the former is at the end of the
stroke. If the piston touched the cylinder-head at the
end of each stroke, it would cause a concussion or
“thump” which would injure these parts. Owing to
the impossibility of constructing machinery with absolute
accuracy, it is therefore necessary to leave a space,
usually from ¹⁄₂ to ¹⁄₄ in. wide, between the piston and
the cylinder-heads, so as to be certain that they will
not strike each other should there be any slight inaccuracies
in the length of the piston-rods, connecting-rods,
frames or other parts.
Question 204.Why is it desirable to open the steam-port
and admit steam at the end of the cylinder towards
which the piston is moving BEFORE the latter has completed
its stroke?
Answer. Because it is essential, in order to insure
a good action of the steam, that the maximum cylinder
pressure should be attained at the very commencement
of the stroke. If the steam-port was not opened
until after the piston had commenced its stroke, some
appreciable time would be consumed in filling the
clearance space and the steam-way with steam.[57] It is
also found, especially if an engine is working at a
high speed, that a slide-valve worked by the ordinary
link-motion will not open the steam-port rapidly
enough to enable steam of the maximum boiler pressure
to fill the space after the receding piston, unless
the valve begins to open the port before the piston
reaches the end of its stroke.
[57] The steam-ways are the passages which lead from the steam-chest
to the cylinder, and are sometimes called steam-ports, but the term
steam-ways is used to distinguish the passages from their openings in
the valve-seat, which latter are more properly called steam-ports.
Another advantage resulting from the pre-admission
of steam consists in the smooth working of the engine
at high speeds, a circumstance which reduces greatly
the wear and tear of the working gear. As the piston
approaches the end of its stroke, the pre-admitted
steam forms a kind of elastic cushion, which is well
calculated to absorb the momentum of the reciprocating
parts at that instant. The pressure due to the
momentum of these parts will, of course, depend upon
their weight and the speed of working, increasing directly
as the square of the speed. It follows from
this that the lead should increase with the speed, and
that it should be greatest at high speeds. As has
been shown before, this condition is fully accomplished
by the ordinary shifting-link motion.
Question 205.Upon what does the admission of
steam into the cylinder depend?
Answer. It depends in the first place upon the opening
of the throttle-valve, and the size of the pipes and
passages through which it is conveyed from the boiler
to the cylinder. In the second place, it depends upon
the time and amount of opening of the steam-port by
the valve.
Question 206.What should be the pressure of the
steam in the cylinder during admission?
Answer. In order that the steam may be used to
most advantage, it should be admitted and maintained
in the cylinder at full boiler pressure during the whole
period of admission. If the opening of either the
throttle-valve or the steam-ports is not sufficient to
allow the steam to flow into the cylinder at full boiler
pressure, the steam is said to be wire-drawn, and
much of the advantage of using it expansively as has
already been explained in answer to Question 59, is
then lost.
Question 207.Why is it difficult to admit and maintain
steam at the full boiler pressure in the cylinder during
admission?
Answer. Because it is necessary to reduce the travel
of the slide-valve in order to cut off the steam “short,”
or soon after the beginning of the stroke of the piston.
When the travel is reduced, the valve opens the port
only a small distance, so that the area of the opening
is not then sufficient to allow the steam to flow into the
cylinder with sufficient rapidity to fill it at full boiler
pressure, especially if the engine is working at a high
speed. Thus, by referring to the table given on page
216 and to the motion curves in fig. 128, it will be
seen that when the steam is cut off at from ¹⁄₄ to ¹⁄₂
stroke, the port is opened for the admission of steam
only from ¹⁄₄ to ¹⁄₂ inch wide. From the curves it will
also be seen that the valve then acquires its maximum
travel and the steam-port its greatest width of opening
very soon after the piston begins its stroke; after
which the port is gradually closed, so that before the
steam is entirely cut off the opening is so much reduced
in area that the steam cannot flow through
it rapidly enough to maintain the steam at full boiler
pressure in the cylinder when the engine is working
at high speeds.
Question 208.What means are used to overcome this
difficulty and thus admit steam at full boiler pressure
when the valve is cutting off short?
Answer. In the first place, the steam-ports are
made from ten to twelve times as long as they are
wide, so that a narrow opening will have a comparatively
large area. In the second place, by giving the
valve lead, not only are the clearance space and the
steam-way filled with steam when the piston begins its
stroke, but the port is then open a distance equal to
the lead. With the ordinary link motion, as has already
been shown, this lead increases as the travel
and period of admission diminish, so that the smaller
the total distance that the port is opened, the greater
is its opening at the beginning of the stroke. As the
steam is usually cut off short when locomotives run at
high speeds, it will be seen that the increased lead
which is imparted to the valve by the shifting link is
an advantage rather than a disadvantage. But while
it is often possible in this way to secure a pressure of
steam in the cylinder at the beginning of the stroke
equal or nearly so to that in the boiler, yet it is almost
impossible to maintain this pressure during the whole
period of admission, when the steam is cut off short
and the engine working at a high speed. To obviate
this evil what is called the Allen valve was designed,
which is represented in fig. 132. This valve has a
channel or supplementary port, a a, which passes over
the exhaust cavity, and has two openings, b, b′, in the
valve-face. When the valve begins to admit or “take”
steam at c, as shown in fig. 133, it will be seen that it
also uncovers the opening b′ at e and admits steam at
b′, which passes through the channel b′ a a b and enters
the steam-port c at b, and in this way there is a double
opening for the admission of steam. The opening b
of the supplementary port is closed as the valve advances,
but when this takes place the steam-port is
uncovered far enough to admit all the steam that is
required. This form of valve is very efficient when
the travel and point of cut-off are very short. It
then gives just twice as much opening as the ordinary
valve for the admission of steam. This improved
valve has been much used in Europe; but, although it
is an American invention, has not received the attention
in this country which its merit deserves.
Fig. 132.
Fig. 133.
Scale ³⁄₁₆ in. = 1 inch.
Question 209.What is meant by the pre-release of
steam?
Answer. It is the release of the steam before the
piston has completed its stroke. If it is confined until
the piston has reached the end of the cylinder, there
will not be time nor will it be possible, with a slide
valve and link-motion, to secure a sufficiently large
opening of the port to permit the steam to escape from
the cylinder before the piston begins its return stroke.
If there were no pre-release, there would therefore be
more or less back pressure on the piston.
Question 210.Upon what does the amount of pre-release
depend?
Answer. First, as has already been explained in answer
to Question 51, on the amount of inside lap; and
second, on the outside lap of the valve and lead of the
eccentrics; and third, on the travel of the valve. The
less the inside lap, the greater the outside lap and consequent
lead of the eccentrics; and the shorter the
travel of the valve, the earlier will be the release.
The proper amount of this pre-release depends upon
the velocity of the piston and the quantity of steam
to be discharged or the degree of expansion. From
the motion-curves in fig. 128 it will be seen that it is
a marked feature of the shifting-link motion that the
pre-release occurs earlier in the stroke as the link approaches
mid-gear, or as the travel of the valve diminishes.
As the link is usually worked near that position
when the engine is run at a high speed, it will be seen
that in this respect again the link-motion is well
adapted for working the slide-valves of locomotives.
Question 211.What governs the period of release?
Answer. The release like pre-release is dependent
upon the amount of inside lap, the outside lap and
consequent lead of the eccentrics, and the travel of the
valve.
The addition of inside lap has the effect of closing
the port earlier than it would be closed without, and
thus shortening the period of release and also of reducing
the area of the opening of the port. This will
be apparent by referring to fig. 128, in which the valve
had ¹⁄₁₆ in. lead. The dotted lines which represent
the edges of the ports in relation to the exhaust edges
of the valve are therefore drawn ¹⁄₁₆ in. from the centre
line a b. If, however, there had been no inside
lap, then the edges of the ports would have conformed
to the line a b. It will be observed that the first curve
crosses the dotted line g g′ at 15¹⁄₂ in. of the forward
stroke, which is the point at which the port is closed to
the exhaust, or where the period of release ends and
compression begins. If there had been no lap and the
line g g′ had therefore occupied the same position as
a b, then the motion-curve would not have crossed it
until the piston had reached 16 in. of its stroke, thus
showing that the period of release had been lengthened
and compression delayed. As the width of the opening
of the port is represented by the distance of the
motion-curve from the right hand side of the line g g′,
which represents the edge of the port, it is obvious
that if there had been no lap, so that the position of
the line representing the edge of the port had occupied
the position of a b, then the space between it and the
motion-curve would have been greater, thus showing
that the port would have been opened wider if there
had been no inside lap. The width of the opening of
the port to the exhaust is in fact always diminished
by an amount equal to the inside lap.
With the same travel, increase of outside lap and
lead shortens the period of release, but has no effect
on the width of the opening of the port to the exhaust.
Increase of travel, with the same outside lap, lengthens
the period of release and also increases the width
of the opening of the port to the exhaust.
Question 212.What governs the period of compression?
Answer. As compression begins when release ends,
or when the port is closed to the exhaust, it is controlled
by exactly the same causes, and as the two
events occur simultaneously, of course whatever shortens
the period of release lengthens that of compression.
Question 213.What effect do the clearance spaces
and steam-ways have upon the compression of the confined
steam?
Answer. By referring to the motion-curves in fig.
128, it will be seen that the steam-port is closed by
the exhaust edge of the valve, or compression begins
some time before the piston reaches the end of the
stroke. The result is that the remaining portion of
the cylinder, through which the piston must move
after the port is closed to the exhaust, is filled with
steam of atmospheric pressure, or possibly a little
above that pressure. As this is confined in the cylinder,
it is compressed by the advance of the piston. If
there was no room between it and the cylinder at the
end of the stroke, then either the cylinder would be
burst or the valve would lift so as to allow the compressed
steam to flow back into the steam-chest. The
clearance and the steam-passages, however, afford considerable
room, into which the confined steam can be
compressed without danger of bursting the cylinder,
or of raising the slide-valve when there is steam in
the steam-chest. As the clearance spaces and steam-ways
must be filled with high-pressure steam at the
beginning of each stroke, it must be obtained either
by taking a supply of “live”[58] steam from the boiler,
or by compressing into the clearance spaces the low-pressure
steam that still remained in the cylinder
when the port was closed to the exhaust. By the latter
process, a certain quantity of steam is saved at the
expense of increased back pressure. It should be
borne in mind also that the total heat of the compressed
steam increases with its pressure, and as this
latter approaches that in the boiler, the temperature
of the former must have been raised from that due
to about atmospheric pressure to nearer the temperature
of that in the boiler. These changes of temperature
which the steam undergoes will affect the surface
of the metal with which the steam is in contact during
the period of compression; it follows from this, that
the ends of the cylinder principally comprising the
clearance spaces must acquire a higher temperature
than those parts where expansion only takes place.
This is an important consideration, since the fresh
steam from the boiler comes first in contact with these
spaces, and by touching surfaces which have thus previously
been heated, as it were, by the high temperature
of the compressed steam, less heat will be abstracted
from the fresh steam, and therefore a less
amount of water will be deposited in the cylinder.[59]
[58] The term “live” steam means steam taken direct from the boiler
and which has not been used in the cylinder or to do any work.
[59] Bauschinger’s Indicator Experiments on Locomotives, published in
Vol. III. of the Railroad Gazette.
It will thus be seen that the effect of compression is
to fill the clearance spaces and steam-ways with compressed
steam before pre-admission begins. As already
stated, this is done at the expense of back pressure in
the cylinder. It must be remembered that all the energy,
excepting that part which is wasted by loss of
heat, friction, etc., which is consumed in compressing
the confined steam, is again given out to the piston by
expansion. The confined steam also acts as an elastic
cushion to receive the piston, just as the steam which
is admitted before the end of the stroke would if there
were no compression. Compression, therefore, has the
effect of saving the quantity of live steam which it
would otherwise be necessary to admit before the end
of the stroke to fill the clearance spaces and steam-ways
and also to “cushion” the piston. As already
stated, the momentum of the piston and other parts
depends upon their weight and the speed at which
they are working, increasing directly as the square of
the speed, from which it follows that the compression
should increase rapidly with the speed, and should be
the greatest at high speeds. As the ports are prematurely
closed to the exhaust with the shifting-link
motion, and as the lead increases rapidly as the link
approaches mid-gear, and the amount of compression
is at the same time correspondingly augmented, it
will be seen that the shifting-link motion fulfills these
conditions very perfectly.
The pressure to which the confined steam will rise
depends of course upon the amount of the period of
compression, and also on the size of the clearance
spaces. As it is possible to have such an amount of
compression that it will exceed the boiler pressure,
and thus raise the valve from its seat and be forced
back into the steam-chest, some care must be exercised
to proportion the one to the other, so that the degree
of the confined steam may not be excessive.
Question 214.How can the effect of the distribution
of the steam upon its action in the cylinder be determined
by experiment?
Answer. As already explained in answer to Question
55, this can be done by an instrument called a
steam indicator.
Fig. 134.
Fig. 135.
Scale 3 in. = 1 foot.
Question 215.What is the construction of this instrument?
Answer. The indicator now ordinarily used is the
Richards indicator, the outside of which is represented
in fig. 134 and a section in fig. 135. It consists of a
cylinder, B, into which a piston, C, is accurately fitted,
but so that it will move freely in the cylinder. The
piston rod is surrounded with a spiral spring, D, the
lower end of which is attached to the top of the piston,
and the upper end to the cylinder cover. When
steam is introduced below the piston it pushes it up in
the cylinder and the spring is compressed. If there
should be a vacuum below the piston, the air above it
will press the piston downward and extend the spring.
This latter occurs only when the indicator is used on
condensing engines. Of course the distance which
the piston is forced up by the steam pressure below it
depends upon the amount of pressure and also on the
tension of the spring; and therefore by attaching a
pencil to the piston-rod so that it can mark on a
moving card in front of it, a diagram will be drawn
which would indicate the steam pressure, as was explained
in answer to Question 55. But there are
some practical difficulties in the way of doing this.
It is found that if the pencil is attached directly to the
piston-rod of the indicator, the distance through which
they must move, in order to make the scale of the diagram
sufficiently large to be clear, is so great that the
momentum of the parts carries them further than the
pressure of the steam alone would move them. The
distance through which the pistons or instruments
move, moreover, makes it impossible that the changes
of pressure should be indicated simultaneously with
the position of the piston; the latter must travel while
the action is taking place, and thus the diagram shows
changes of pressure later or more gradually than they
occur.[60] To overcome these and other difficulties, the
piston-rod of the indicator which we have illustrated
is attached at h to the short arm of a lever, F G, and
to the end of the long arm a piece, F I, is attached,
which carries a pencil, J. By this means the piston
has only one-fourth of the motion that it imparts to
the pencil, so that the momentum of the moving parts
is comparatively slight. If the pencil was attached
directly to the end of the lever, it is obvious that it
would move in the arc of a circle, and that this would
be a source of error in the diagram. To avoid this
the pencil is attached to what is called a “parallel
motion.” This consists of a coupling-rod, F I, which
connects the ends of two levers, F G and I H. The
centre of the rod F I, to which the pencil is attached,
will with this arrangement move in a straight line.
The levers and all the parts are of course all made as
light as possible, so that their weight will have little
effect on the motion of the indicator piston.
[60] Richards’ Steam Indicator, by Charles T. Porter.
The paper or card on which the diagram is drawn
is wrapped around a brass cylinder, A A. This cylinder
is made to revolve part of the way around by a
strong twine, a b, which is wrapped around a pulley, b,
at the bottom of the cylinder. The twine is attached
to a lever, similar to that shown in fig. 30, which receives
a reciprocating motion from the piston of the
engine. The twine can of course move the cylinder
only in one direction, and therefore a coiled spring
similar to a clock spring is placed inside of the cylinder
to draw it back when the twine is relaxed. In
this way the paper cylinder or drum receives a part of
a revolution at each stroke of the piston, and moves
simultaneously with it. This drum is used instead of
a flat card, on account of the practical difficulties of
employing the latter. The motion of the paper on this
drum will, however, be exactly the same in relation to
the pencil as the motion of a flat card would be.
Fig. 136a.
The method of attaching an indicator to a locomotive
is represented in fig. 136a. It will be seen from
this that it is placed over the center of the steam
chest and connected to each end of the cylinder with
³⁄₄-inch pipes. A globe valve was in the case represented
placed on each side of the indicator, so that it
could be put into communication with either end of
the cylinder, or could be completely shut off from both.
A better plan, however, is to have a three-way cock at
the point where the horizontal pipe connects with the
vertical one leading to the indicator, as the passages
in a three-way cock are more direct than those in
globe valves. The arrangement of the levers for
giving motion to the indicator drum, and of the seat,
which is very requisite for the experimenter, will be
readily understood from the engraving without further
explanation. It is thought by some engineers that
the indicator should be applied as near to each end of
the cylinder as possible. It is believed, however,
that if the pipes, cocks, and their connections are made
large enough so as not to impede the motion of the
steam, no appreciable error will arise from the method
illustrated in fig. 136a.
Question 216.What should be the form of an indicator
diagram, if the steam is distributed by a link motion
so as to produce the best practicable action in the cylinders?
Answer. It should approximate to that shown in fig.
136b. In this diagram the vertical lines represent
inches of the stroke, and the scale on the left the
steam pressure in pounds per square inch. The atmospheric
and vacuum lines are also indicated, as already
explained in answer to Question 55. The points
at which the different periods of the distribution begin
are indicated by the letters a, b, c, d, e and f. These
are in the order in which they occur: a, pre-admission;
b, admission; c, expansion; d, pre-release; e,
release; and f, compression. The lines forming the
outline of the diagram will be designated for convenience
of description as follows:
The line from a to b, the admission line.
The line from b to c, the steam line.
The line from c to d, the line or curve of expansion.
The line from d to e, the exhaust line.
The line from e to f, the line of back pressure.
The line from f to a, the line or curve of compression.
Fig. 136b.
The diagram represents a distribution of steam produced
by a valve having ⁷⁄₈ in. outside and ¹⁄₁₆ inside
lap, and operated by the link motion represented in
fig. 103. The eccentrics have 5 in. throw, and the
steam-ports are 1¹⁄₄ and the exhaust 2³⁄₄ in. wide. The
valve as shown by the diagram is cutting off at 8 in.,
or one-third of the stroke. Pre-admission begins when
the piston still has ¹⁄₂ in. to move before reaching the
end of its stroke. Admission of course begins with
the stroke, expansion at 8 in., pre-release at 18¹⁄₂ in.,
release at the end of the stroke, and compression at
17¹⁄₂ in. of the return stroke. The valve is supposed
to be set without any lead, or “line and line,”[61] as it is
called at full stroke. When the steam is cut off at 8
in. of the stroke, the valve has 2⁵⁄₈ in. travel and ³⁄₁₆ in.
lead. The steam pressure in the boiler is supposed to
be 100 pounds above the atmosphere. Of course, when
the valve cuts off at different points of the stroke, the
periods of distribution will be somewhat changed; but
from the above diagram the principal features of a
good distribution can be explained.
[61] That is, the steam edges of the valve correspond with the steam
edges of the port at the beginning of the stroke.
These are: First, that the steam pressure should rise
rapidly during the period of pre-admission, so that
there will be full boiler pressure in the cylinder at the
beginning of the stroke. When this occurs, the pre-admission
line will rise from a to b, to such a point at
b which will indicate full boiler pressure in the cylinder.
The same pressure should then be maintained
in the cylinder during the whole period of admission,
and the admission line from b to c should therefore be
a straight horizontal line, as shown in fig. 136b. When
expansion begins, the pressure will fall, as was explained
in answer to Question 55. The expansion line
should approximate a hyperbolic curve, but if there is
much loss of heat by radiation or other causes, the
diagram will fall considerably below the theoretical
curve. With cylinders well protected and with dry
steam the expansion line will fall slightly below a hyperbolic
curve at the beginning of the period of expansion,
and rise above it during the latter part of the
same period. The reason of this is that the cylinder
is heated by the admission of live steam of comparatively
high pressure and temperature, so that, when
the pressure becomes reduced by expansion, a part of
the water which is condensed in the cylinder will be
re-evaporated by the heat in the latter. From the
point of the pre-release, d, to the end of the stroke, e,
the exhaust line should fall rapidly, so that there will
be no pressure behind the piston during its return
stroke. To explain the theoretical form of the exhaust
line would lead us into a very abstruse discussion,
which would be out of place here. It will be
sufficient for our purpose to call attention to the fact
that the pre-release should allow all the steam in the
cylinder to escape before the piston reaches the end of
the stroke, so that the back pressure during the return
stroke may be as low as possible. It is, however,
only at comparatively slow speeds that the steam in
locomotive cylinders escapes during the period of pre-release,
so that the back pressure is reduced to that of
the atmosphere. It is necessary in locomotives, as
has already been explained, to contract the area of
the blast orifices or exhaust nozzles, in order to stimulate
the draft through the fire, so that the steam
cannot escape with sufficient rapidity to reduce the
back pressure to that of the atmosphere if the engine
is running fast. Of course every pound of back pressure
on the piston is so much loss of energy, and a
reduction of the amount of work done by the engine;
but it is a sacrifice which must be made in order to be
able to generate the requisite quantity of steam. In
studying the distribution of steam, however, every
effort should be made to reduce the back pressure as
much as is practicable, and yet maintain a sufficient supply
of steam, and therefore the line of back pressure
should conform as closely as possible to the atmospheric
line. The compression line should be a hyperbolic
curve, beginning with the period of compression.
In calculating both the compression and expansion,
allowance must be made for the clearance space and
steam-way. In a cylinder like that illustrated in fig.
92, their contents would be about equal to that of two
inches of the cylinder. Therefore, when steam is cut
off at 8 in. of the stroke, instead of having a quantity
of steam which will fill a cylinder 16 in. diameter and
8 in. long, we have as much as would fill a cylinder of
that diameter and 10 in. long. The same thing is
true of the compression. This must occur in the above
example when the piston has 6¹⁄₂ in. more to move before
completing its stroke. There is therefore a quantity
of steam in front of it sufficient to fill a cylinder
8¹⁄₂ in. in diameter. This steam is of course compressed
by the advance of the piston, and if its pressure when
compression begins is the same as that of the atmosphere,
then it will be 0.9 lbs. above it when the piston
has only 6 in. to move and 3.2, 6.2, 10.5, 16.9, and
27.5 lbs. effective pressure when the piston has 5, 4,
3, 2 and 1 inches to move respectively, and when pre-admission
begins, the pressure will have risen to 48.7
lbs. If the back pressure is above that of the atmosphere,
of course the compression will be correspondingly
increased. It will also be seen that, without any
or with very little clearance space, the compression
would at the end of each stroke rise above the boiler
pressure. It being a peculiarity of the ordinary shifting-link
motion that as the period of admission is reduced
that of compression is lengthened, the latter
becomes very excessive when the steam is cut off at
less than one-third or one-fourth of the stroke.
Question 217.In what respect would a diagram made
by an indicator differ from the theoretical form represented
in fig. 136b?
Answer. It would be drawn with less exactness;
that is, the corners instead of being sharply defined,
as in fig. 136b, would be more or less rounded, as in fig.
137, and the curves and straight lines would vary
somewhat from the exact mathematical form indicated
in fig. 136b. The higher the speed at which the engine
is working when the diagrams are taken, the
greater will be the variation from the theoretical form.
Fig. 137.
Question 218.If the amount of pre-admission is
insufficient, how will it be shown in the indicator diagram?
Answer. The effect of too little pre-admission is to
lower the pressure of the steam at the beginning of
the stroke, and at high speeds there will not be time
enough nor sufficient opening of the steam-port to supply
the deficiency after the stroke has commenced.
The corner of the diagram at b will then be very much
rounded, as shown in fig. 138. This is apt to be the
case when steam is admitted during a considerable
part of the stroke, as a shifting-link motion then gives
less lead than when it is worked nearer mid-gear. If
the steam is cut off short, then the pressure in the
cylinder during admission is very much below boiler
pressure, and is apt to fall rapidly after the commencement
of the stroke, as shown in fig. 138.
Fig. 138.
Question 219.If the opening of the steam-ports during
admission is too small, what will be the form of the
diagram?
Answer. The effect will be very much the same as
that produced by too little pre-admission or lead; that
is, the pressure in the cylinder will be much lower
than in the boiler and will fall rapidly during the
periods of admission, as shown in fig. 138.
Question 220.What defects will be indicated by the
expansion curve of indicator diagrams?
Answer. If the cylinders are not well protected, and
there is much loss of heat from radiation, there will
be a rapid fall of pressure during the period of expansion,
which will be shown by the expansion curve falling
below the theoretical curve shown in fig. 136b. If,
on the contrary, the indicator curve is much above the
theoretical curve, it may be caused by a leak in the
valve. As steam is quite as likely to leak from the
steam-port into the exhaust as from the steam-chest
into the steam-port, a valve which is not tight may
produce just the contrary effect upon the indicator
diagram. As it is usually quite easy to detect a leak
in the valve by other means, the use of the indicator
for this purpose is unnecessary. Attention is called
to it, however, to show the impossibility of getting
results of any value with the indicator if the valves
are not steam-tight.
Question 221.What should be observed regarding the
exhaust line of the indicator diagram?
Answer. The most important point to be observed
is, whether the pressure at the end of the stroke is
reduced as low as possible, as at high speeds it is usually
much more difficult to exhaust the steam from
than to admit it into the cylinder. As already stated,
the blast in the chimney makes it almost impossible
to exhaust the steam to atmospheric pressure when
the locomotive is running fast. If the steam is released
too late in the stroke, as already explained,
there will not be time enough nor sufficient opening
of the port to allow the confined steam to escape from
the cylinder before the end of the stroke, and this will
be indicated on the diagram by the space between the
line of back pressure and the atmospheric line during
the commencement of the return stroke, as shown in
fig. 138.
Question 222.What should be observed regarding the
line of back pressure?
Answer. The most important point is, that it should
approximate as closely as possible to the atmospheric
line, as all the back pressure not only diminishes the
efficiency of the engine, but is a total loss of energy.
Too much inside lap will increase the amount of back
pressure, but generally it is more influenced by the
area of the blast orifices than by any other cause.
Every effort should be made, therefore, to have them
as large as possible and yet have the boiler make as
much steam as is needed.
When only one blast orifice is used for both cylinders,
it often happens that when the steam is exhausted
from the one cylinder it “blows” over into the
other, and thus produces an additional amount of back
pressure. This is shown by a rise or “hump” in the
line of back pressure, as indicated in fig. 138.
Question 223.Can the amount of compression which
is needed be determined by calculation?
Answer. Yes; but it involves more abstruse principles
of mathematics than it is thought best to introduce
here. Some of the reasons can, however, be
given, which will make the subject clearer, and enable
the reader, if he has sufficient knowledge of mathematics,
to investigate the subject still further.
Fig. 140.
In the first place it is a well-known fact that the
motion of a piston in the cylinder of a steam engine
is not a uniform one, but increases in speed from the
beginning of the stroke to the middle, and diminishes
in speed from the middle to the opposite end. The
cause of this is that the crank revolves at a uniform
speed during the entire revolution, but the piston
moves much less at the beginning of the stroke, with
a given amount of revolution of the crank, than it
does at the middle. This is shown in fig. 140, in
which A is a cylinder and B the piston and a b c d
the path of the crank. Now while the crank moves
from a to 1, or ¹⁄₁₂ of a revolution, the piston has moved
1³⁄₈ in., or a distance equal to that from a to 1′ or to the
base of a perpendicular drawn from 1 to the centre
line a c. While the crank moves from 1 to 2, or
through the second twelfth of a revolution, the piston
has moved from 1′ to 2′, or 4³⁄₈ in., or 2³⁄₄ in. further
than during the first twelfth of the crank’s revolution.
During the third twelfth of the revolution the piston
moves from 2′ to 3′, or 6 in., thus showing that it
continues to increase in the distance moved during
each period of the revolution of the crank until the
latter has made a quarter revolution. The speed of
the piston then begins to diminish until it reaches
the end of the stroke. It is slightly affected by the
angularity of the connecting-rod, as already explained,
but for the present this is disregarded. It is obvious
now that if the momentum, or actual energy stored
up in the piston and other reciprocating parts after
they have passed the middle of the stroke, added to
the pressure behind the piston, is greater than the resistance
offered by the crank, the motion of the latter
will then be accelerated and thus conveyed to the
moving engine and train. If, however, there is any
momentum in the piston when it reaches the end of
the stroke, evidently it can exert no power to cause
the crank to revolve, but must be expended by producing
a pressure on the crank-pin and thus on the
axle-boxes. Not only will such a pressure not cause
the crank to revolve, but it will be more difficult to
turn the crank with such a pressure against it than
it would be without. The momentum of the piston
and other reciprocating parts at the dead point therefore
creates a resistance to the movement of the crank
instead of helping to turn it. It will also be observed
that after the crank has moved slightly from the dead
point, any pressure on the piston will exert very little
force which will tend to turn the crank. In fact the
nearer the piston is to the end of the stroke the greater
is the proportion which the friction of the crank-pin
and axle bears to the useful effect of the strain in
causing the crank to turn. Calculation shows that
for about three degrees on either side of the dead
points the effect of pressure on the crank-pin is actually
to retard the engine. If now the piston reaches
the end of the stroke with a certain amount of unexpended
momentum stored up in it, if this energy is
expended by producing pressure on the crank, then it
will not only be a waste of energy but a double waste
by retarding the motion of the crank. If, however,
this energy can be absorbed by compressing steam
which will fill the clearance spaces, it will not only
prevent the retarding effect referred to, but the energy
in the piston and other parts will be converted
into steam pressure, which will be given out in useful
work during the next stroke. It would, of course, be
impossible to arrest the motion of the piston instantly,
and therefore its momentum is gradually absorbed
from the time compression begins until it reaches the
end of the stroke. As the energy of a moving body
is equal to its weight multiplied by the square of its
speed, it is obvious that to overcome this a different
amount of compression would be required for each
speed, and also that it must be adjusted to the weight
of the moving parts. Such exact adaptation is not
practicable on locomotives, nor does the link motion
enable us to alter the amount of compression with so
much exactness: but the explanation shows the value
of increasing the amount of compression with the
speed, which fortunately the peculiarities of the shifting-link
motion enable us to do without difficulty.
Fig. 139.
Question 224.What cause produces the form of diagram
represented by Fig. 139?
Answer. It is produced by excessive compression,
which causes the pressure in the cylinder to rise above
boiler pressure before pre-admission begins. As soon
as the port is opened, part of the steam in the cylinder
flows back into the steam-chest, and thus the
pressure is reduced, as shown by the diagram.
Question 225.How can we determine whether the
steam is distributed in the cylinders to the best advantage,
and how can we discover the fault, if there is one, in the
link motion?
Answer. The indicator will show the action of the
steam in the cylinder, and motion-curves drawn with
the instrument described in answer to Question 192
will show the exact movement of the valve. By comparing
the indicator diagram with the motion-curves,
the one will show the defects in the other.[62]
[62] See description of Richards’ Improved Steam Engine Indicator, with
directions for its use, by Charles T. Porter, London.
Question 226.To what extent can the movement of
the valve be modified by alterations in the proportions of
the link motion?
Answer. The motion of the valve is susceptible of
an almost infinite number of changes, by different variations
and combinations of proportions of the working
parts of the link motion. These changes are,
however, limited by the general laws which govern the
motion of eccentrics, and therefore cannot influence
the motion of the valve beyond certain limits. Hardly
any variation can be made either in the proportions or
arrangement of the working parts which will not have
some influence upon the movement of the valve. Aside
from the proportions of the valve itself, which have
already been discussed, the throw of the eccentrics,
the length of the rods and of the link, the point of
connection of the rods with the link, the point of
suspension, the position of the lifting shaft, the length
of the arms, the length and position of the rocker arms
will each of them effect the distribution of steam.
The number of combinations of all these different
proportions is of course almost infinite, and therefore
any full discussion of them will be impossible here.
Question 227.What are the most important points
which require attention in designing a link motion?
Answer. It should be proportioned so that—
First, the lead and the period of admission should
be the same for each end of the cylinder, for each
point of cut-off, and, if possible, in back as well as
forward gear.
Second, the width of opening for both admission
and exhaust should be as large as possible when steam
is cut off short.
Third, the exhaust or pre-release should occur early
enough and be maintained long enough to reduce back-pressure
as low as possible.
Question 228.How can the lead and period of admission
be equalized?
Answer. It is impossible to make the periods of admission
absolutely alike for every point of cut-off in
both fore and back gear. It is therefore customary to
disregard the back gear, as engines are worked but
little with the link in that position. Even for forward
gear the periods of admission cannot be made exactly
alike for each end of the cylinder and for each point
of cut-off, and therefore it is usual to make the periods
of admission alike for half-gear forward, in which position
the link is worked most.
The periods of admission for the front and back
ends of the cylinder can be changed most in relation to
each other by altering the position of the point of suspension
on the link. This can be done either by
moving this point up or down, or horizontally. Usually
links are suspended from a point halfway between the
points of connection of the eccentric-rods and from ¹⁄₄
to ³⁄₄ in. back of the centre line of the slot in the link.
A somewhat better distribution can be secured by
suspending it about 3 in. above the centre, but the
suspending link must then be made so short that it
is subjected to very great strains by the motion of the
link, and this evil is usually considered much greater
than the advantage which is gained thereby in the
more equal distribution. The point at which the
upper end of the suspension link is hung also influences
the relative amount of admission front and back.
This point, of course, varies as the end of the lifting
arm is raised or lowered. In designing valve gear it
is usually tested by a full-sized model, which will
show the exact motion of all the parts. The best position
for the lifting shaft and the length of its arm
can be determined perhaps most satisfactorily by
placing the link in full gear forward, then moving the
point of suspension of the upper end of the link-hanger
horizontally so that the front and back admission will
be alike, and then marking this position. The same
process should then be repeated for half gear and for
the shortest point of cut-off. If the position of the
lifting shaft and the length of its arm are then so arranged
that the end of the latter will move through
the three points which have been thus determined,
the admission will be very nearly equal for each end
of the cylinder. Usually, however, it is impossible to
arrange the shaft and arm so that they will conform
exactly to these conditions, and therefore an approximation
is made which will come as near as possible to
what is required. It may be stated, however, that
the lifting shaft should be kept as low as possible,
so as not to interfere with the eccentric-rods. In
some cases the shaft has been suspended from the
boiler, so that the outside eccentric-rod would work
past or over the end of the lifting shaft, thus allowing
the latter to be located lower than would otherwise be
possible.
Question 229.Which parts of the link-motion have
the greatest influence on the distribution of steam?
Answer. The lap of the valve and the throw of the
eccentrics. The effect of any change of these upon
the distribution is very similar to that produced if a
single eccentric is used, which was explained in the
answers to Questions 49, 50 and 52.
Fig. 141.
Question 230.What is the effect upon the admission
of increasing the throw of the eccentrics with the same
lap?
Answer. As already explained, the effect is to increase
the period of admission, or in other words to cut
off later in the stroke, and also to increase the width
of the opening of the steam-port or the distance which
the valve throws over the port. This has an important
influence upon the admission, when the link-motion is
used.
Question 231.What is meant by the angular advance
of the eccentrics?
Answer. It is the angle which a line, e f, fig. 141,
drawn through the centre of the axle and the centre
of the eccentric makes with a vertical line a b, when
the crank is on one of the dead-points or centres.
Thus in fig. 141 the crank A is represented on the
front centre. In order to give the valve the necessary
lead the eccentric must be moved ahead of the vertical
line a b. The angle c which the line e f (drawn
through the centre of g of the eccentric and f of the
axle) makes with the vertical line is called the angular
advance.
Question 232.What is meant by linear advance?
Answer. By linear advance is meant the distance
which the valve has moved from its middle position
at the beginning of the stroke of the piston. This,
when the two rocker arms are the same length, is the
same as the distance of the centre of the eccentric g
from the vertical line a b, fig. 141.
Question 233.Why does the cut-off occur earlier
with an eccentric having a short throw than with one
which gives more travel to the valve?
Answer. Because it is necessary to give the eccentric
with the short throw more angular advance in
order to give the valve the required lead. This is
illustrated in fig. 142, in which a section of a valve,
V, and ports c, g, and d, are represented. In order to
simplify the diagram as much as possible the rocker is
left out and the valve is supposed to be moved by the
rod R directly from the centre a of the eccentric.[63]
The effect of the angularity of the connecting rod
and eccentric rod is also neglected. The circle a b e f
represents the path of the centre of an eccentric
having 5 in. throw, and h i j the path of one having
3¹⁄₂ in. throw. In order to give the valve the required
lead, which is supposed to be just line-and-line at
the beginning of the stroke, the linear advance of the
valve must be equal to the lap, or ⁷⁄₈ in. If therefore
we draw a line, p a, parallel to the vertical centre line,
e k, and ⁷⁄₈ in. from it, the intersection of p a at a and
h with the paths of the eccentric will be the centres
of the eccentrics. If through these centres and the
centre of the circle, lines, o a and o p, be drawn, the
angles which they make with the vertical e k will be
the angular advance. It will be seen from these lines
that in order to give the valve the required lead it is
necessary to give the eccentric with the small travel
more angular advance than is necessary for the one
with the larger throw. It is obvious, too, that when
the centre of the larger eccentric has reached the point
b the valve will have received its greatest travel, and
that when it reaches p the steam-port c will again be
closed or the steam cut off. If the small eccentric is
employed, the valve will then have its maximum travel
when the centre h reaches s, and the port will be closed
when it reaches i. By drawing lines, o p and o n,
through i and p, it will be seen that from the beginning
of the stroke until the steam is cut off, if the
large eccentric is employed, it, and consequently the
shaft and crank, must move over an angle measured
by the arc q t p. If the small eccentric is used, it and
the crank must move through an angle measured by
the arc u t n. In other words, the crank must turn a
considerably greater distance before steam is cut off
with an eccentric having a large than with one having
a small throw.
[63] It will be seen that this causes the position of the centre of the eccentric
to be reversed.
Fig. 142.
Fig. 143.
Scale ³⁄₁₆ in. = 1 inch.
It is also quite obvious from fig. 142 why the port
is opened a shorter distance with a small than with a
large eccentric. The distances o s and o b are equal
to half the throws of the eccentrics, or 1³⁄₄ and 2¹⁄₂ in.
The linear advance o r is in both cases ⁷⁄₈ in., and therefore
after the port begins to open the valve will be
moved by the small eccentric a distance which is equal
to 1³⁄₄ - ⁷⁄₈ = ⁷⁄₈ in., and by the large one 2¹⁄₂ - ⁷⁄₈ = 1⁵⁄₈ in.
Fig. 144.
Scale ³⁄₁₆ in. = 1 inch.
Question 234.What is the effect on the admission of
giving an eccentric with a small throw the same angular
advance as one with a large throw, and then reducing the
lap of the valve so that the lead will be the same in both
cases?
Answer. The admission and the cut-off will then
occur at the same points of the stroke, but the ports
will not be opened so wide. This is illustrated in fig.
143, in which the paths of two eccentrics having the
same throw as those in fig. 142 are represented. The
centre, a, of the larger eccentric is represented in the
same position in fig. 143 as in fig. 142. If a line is
drawn from the centre of the larger eccentric to that
of the axle, and if the centre, h, of the smaller eccentric
is located on the intersection of this line with the
circle representing its path, then the smaller eccentric
will have the same angular advance, but the linear
advance measured by the distance o t will be only ⁵⁄₈
in. If the valve have the same lap as in fig. 142, its
steam edges at the beginning of the stroke, if the
small eccentric is employed, will occupy the position
represented by the dotted lines A and B. If these
edges are cut off, as shown by the full lines and shading,
then the valve will have the same lead as in fig.
142. It is obvious, too, that if the smaller eccentric
has the same angular advance it will reach the
point v, at which, with the reduced lap, the steam will
be cut off, at the same time that the centre, a, of the
large eccentric will reach p, at which point it cuts off
the steam with the valve having the large lap. There
is, however, this difference in the distribution, that in
the one case the valve opens the port a distance equal
to t s, and in the other a distance equal to r b. As o
t is equal to the linear advance of the small eccentric,
or ⁵⁄₈ in., and o s to half the throw of the eccentric, or
1³⁄₄, t s is equal to 1³⁄₄ - ⁵⁄₈ = 1¹⁄₈ in. The distance r b, as
shown above, is equal to 2¹⁄₂ - ⁷⁄₈ = 1⁵⁄₈ in., so that the
effect produced upon the admission of using an eccentric
with a small throw and corresponding amount of
lap is, that the ports are not opened so wide as with
an eccentric having a larger throw.
Fig. 145.
Scale ³⁄₁₆ in. = 1 foot.
Question 235.How do eccentrics with a short throw,
and valves with a corresponding amount of lap, affect the
admission with a link motion as compared with eccentrics
having a larger amount of throw and greater lap of valve?
Answer. The chief difference is that the ports are
not opened so wide for the same period of admission.
Thus in fig. 144 is a series of motion-curves drawn
with a model of a link motion like that illustrated in
fig. 103. The eccentrics had 5 in. throw, and the
valve ⁷⁄₈ in. lap outside and ¹⁄₁₆ in. inside. Fig. 145
represents a series of curves, drawn with the same arrangement
of valve-gear, excepting that the eccentrics
had 3¹⁄₂ in. throw and the valve ¹⁄₂ in. lap. In both
cases the curves represent the motion of the valve
when cutting off at the same point of the stroke. The
following table will show the relative amount of opening
of the port.
[64] The valve throws over 1³⁄₄ in. at this point.
It will be seen from this that the eccentric with 5
in. throw gives a greater width of opening for every
point of cut-off than the one with 3¹⁄₂ in. throw. For
the higher admissions this is not important, but when
steam is cut off short it will be observed that the width
of the opening is very small. At high speeds the
small opening is a great disadvantage.
Question 236.Has it been determined what amount
of opening is required for given speeds of the piston?
Answer. Not with any degree of accuracy. It is
customary to make the area of the ports about one-tenth
that of the piston. It is certain, however, that
with steam-ports of this proportion an opening considerably
less than their whole area is sufficient to maintain
steam at boiler pressure in the cylinders. One of
the defects of the link motion is that the opening of
the port is very small when the steam is cut off short.
It is best, therefore, to secure the largest practicable
opening of the ports for the lower points of cut-off.
Question 237.What are the proportions of the valves
and eccentrics used in the ordinary practice in this country?
Answer. The following report made by a committee
of the Master Mechanics’ Association will show the
proportions used on thirty-five different railroads, and
is a fair indication of the common practice.
TABLE
Outside Lap
Inside Lap
Travel of Valve
Lead in full Gear
Showing the amount of lap, lead and travel of the valves
of locomotives used on 35 of the railroads in the united states and canada.
in.
in.
in.
in.
For
locomotives
running
express
pass.
trains
25
use
⁷⁄₈
¹⁄₈
5
¹⁄₁₀
„
„
„
„
„
„
6
„
³⁄₄
¹⁄₁₆
4
³⁄₄
¹⁄₈
„
„
„
„
„
„
4
„
1
¹⁄₄
¹⁄₄
5
¹⁄₈
„
„
„
accom.
„
„
20
„
³⁄₄
³⁄₈
5
¹⁄₁₀
„
„
„
„
„
„
10
„
⁷⁄₈
¹⁄₁₆
5
¹⁄₂
¹⁄₁₆
„
„
„
„
„
„
5
„
⁵⁄₈
³⁄₁₆
4
¹⁄₂
¹⁄₈
„
„
„
heavy freight
„
19
„
³⁄₄
¹⁄₁₆
5
¹⁄₁₀
„
„
„
„
„
„
11
„
⁵⁄₈
¹⁄₈
4
¹⁄₂
¹⁄₁₆
„
„
„
„
„
„
5
„
¹⁄₂
³⁄₁₆
4
³⁄₄
¹⁄₁₀
Question 238.What should be the width of the
bridge between the steam and exhaust ports?
Answer. It is usually made about the same thickness
as the sides of the cylinder, in order to secure a
good casting; but sometimes it is necessary to make
it wider, in order to prevent steam from escaping from
the steam-chest into the exhaust, which is apt to be
the case if a valve has little lap and a long travel.
Question 239.What determines the width of the
exhaust-port?
Answer. The throw of the valve. This will be clear
if we refer to fig. 146, which represents a valve with a
travel of 5¹⁄₂ in. It will be seen that when it is in the
extreme position in which it is shown the width A
of the opening of the exhaust-port is very small. If
this opening is contracted too much it will of course
interfere with the free escape of the exhaust steam.
It is therefore best to make the exhaust-port so wide
that with the greatest travel of the valve the width of
its opening will be either quite or very nearly equal to
the width of the steam-port.
Fig. 146.
Scale ³⁄₁₆ in. = 1 foot.
Fig. 148.
Fig. 147.
Scale ³⁄₄ in. = 1 foot.
Question 240.Where is the reverse lever located and
how is it constructed?
Answer. It is located on the foot-board[65]K′ K′, as
shown in plate II. It consists of a lever O, O, with the
fulcrum at the lower end. The reverse-rod e k, which
connects the lever with the vertical arm k of the lifting-shaft,
is attached above the fulcrum of the reverse
lever. Figs. 147 and 148 represent side and end
views of the lever on an enlarged scale and with some
of the details attached which are omitted on plate II.
C, C are two curved bars, which in this country are
usually called quadrants, but in England are called
(and more properly) sectors. These are placed on each
side of the reverse-lever and are fastened to some portion
of the engine. They have notches, n, n, n, cut in
them to receive the latch L, which slides in a clamp, H,
and holds the reverse-lever in the notches in which it
is placed. This latch is operated by a trigger, D, which
is grasped by the locomotive runner when he takes
hold of the handle A of the reverse-lever. The trigger
works on a pin, E, as a fulcrum and is attached to the
latch by a rod, r r. When the trigger is pressed up
against the handle, the latch is raised out of the
notches by the rod r r, and is pressed into them again
by the spring s when the trigger is released. F is a
set-screw which presses against a gib, G, and is intended
to keep the latch tight and prevent the reverse-lever
from shaking.
[65] The foot-boardK′ K′, plates
2 and 3, is a platform for the locomotive
runner and fireman to stand on and is located at the back end of the
engine.
Question 241.How are the notches in the sector arranged?
Answer. They are usually arranged so that the steam
will be cut off at some full number of inches of the
stroke when the reverse-lever is in each one of the
notches. They are therefore located so that the steam
will be cut off at 6, 9, 12, 15, 18 and 21 inches, or at 6,
8, 10, 12, 15, 18 and 21 inches of the stroke. A notch
is also placed so as to hold the link in mid-gear. In
some cases as many notches as there is room for are
put into the sectors. The latter seems to be much the
best plan, as it gives more gradations in which the
valve-gear can be worked, and it is a matter of no consequence
whatever in the working of an engine whether
the steam is cut off at some full or some fractional
number of inches of the stroke. By referring to fig.
144 it will be seen how very great the difference of the
distribution of steam must be, as indicated by the 5th,
6th and 7th motion-curves.
Question 242.How long should the reverse-lever be?
Answer. The lever should be sufficiently long so
that in throwing the link from full gear forward to
full gear backward the handle A will move not less
than four times the distance that the link is moved.
It is much better to give the end of the handle A five
or even six times the motion of the link, as there will
then be a much easier action in reversing the engine.
This will also make it possible to use longer sectors,
and give room for more notches.
Question 243.What provision is made in the reversing
gear for overcoming or neutralizing the weight of the
link and other parts of the valve-gear?
Answer. Their weight is counterbalanced by the
pressure of a spring of some kind. In fig. 103 the
two volute springs enclosed in a case, H, are used for
this purpose. These are compressed by the rod m, which
is attached to a short arm l, on the reverse shaft A,
when the link is lowered, and consequently the tension
of the spring resists the weight of the link when
the latter is down or in forward gear. Different kinds
of springs are used for this purpose and sometimes are
attached to the reverse-lever instead of to the lifting-shaft.
Question 244.What is meant by “setting” a slide-valve?
Answer. It is to fasten the eccentrics in the right
position on the axle and to adjust the length of the
eccentric-rods and valve-stem so that the valves will
give the required distribution of steam.
Question 245.How are the valves of a locomotive
set?
Answer. After the wheels, axles, main connecting-rods
and valve-gear are connected together, put the
rocker-arm in its middle position, and lengthen or
shorten the valve-stem so that the valve will be in the
centre of the valve-face. Then place the crank on
the forward centre and the full part of the forward
motion eccentric above and that of the backward motion
eccentric below the axle, and fasten them to the
axle temporarily by tightening up the set-screws.
Then throw the link down until the block comes opposite
to the end of the eccentric-rod, and turn the
wheels,[66] and at the same time, observe whether the
travel of the valve is equal to the throw of the eccentric
and also whether it travels equally on each side of
the centre of the valve-face. If its travel is greater
than the throw of the eccentric, raise the link up; if
less, lower it down until the two are just equal, and
then mark the position for the notches on the sections
or quadrants to receive the latch of the reverse-lever.
If the valve does not travel equally on each side of the
centre of the valve-face, either lengthen or shorten the
eccentric-rod, as may be necessary. Repeat this operation
for the backward motion, by raising the link
up until the block is opposite the end of the lower
eccentric-rod. After having done this, go over the
whole process again to see whether it is all correct.
Now with the crank on the forward centre, and the
link in full gear forward, loosen the set-screws in the
forward eccentric, and move it around the axle so that
the valve will have the required lead and then fasten
it again. Now raise the link up into full back gear,
and set the backward eccentric in the same way. Then
turn the wheels so as to bring the crank on the back
centre, and observe whether the lead is correct for the
back end of the cylinder. If it is not, lengthen or
shorten the valve-stem or eccentric-rod so as to make
the lead alike at both ends, and if it is then too much
or too little, it can be increased or diminished by
moving the eccentrics on the axle.
[66] This can be done by moving the engine on the track, or by raising
it off its wheels, so that the latter can be turned without moving the
former. In some shops a pair of rollers is put in the track so that by
placing the driving wheels on them they can be turned without any difficulty.
Great care must be taken in setting valves to be
sure that the cranks are exactly on the centres or
dead points, and it is impossible to set them in that
position with sufficient accuracy from the motion of
the piston or cross-head, and therefore the centres of
the crank-pins should always be set so as to conform
to a line drawn through the centre of the cylinder and
the axle. When the cylinders are horizontal, it is of
course only necessary to place the cranks on a horizontal
line drawn through the centre of the axle.
When the valves are set it should also be noticed
whether the axle-boxes (whose construction will be
explained hereafter) are in the centre of the jaws, and
if not they should be moved to the centre by driving
wooden wedges between them and the frames,
either above or below, as may be required. The position
of the boxes has a very material influence on the
valve-gear.
If it is intended to lay off the notches on the sectors
so as to cut off steam at certain definite points of the
stroke, these points should be laid off in the guides
from the motion of the cross-head. The latter being
placed in any of the required positions at which steam
is to be cut off, the reverse-lever should then be moved
so that the link will just close the admission port.
The lever can then be clamped to the sectors, and the
wheels turned so as to show whether its position is
correct for each end of the stroke. As before stated
it is impossible to get the ordinary link-motion to cut
off at exactly the same points at both ends of the cylinder,
but a very close approximation can be made by
proportioning the different parts properly. As has
already been stated, it is believed to be a much better
plan to put as many notches in the sectors as possible,
than to locate them for certain definite points of the
stroke.
In setting the valves of locomotives, care must be
taken to turn the wheels forward for the forward motion
and backward for the backward motion.
After the valves are set the position of the eccentrics
on the shaft should be marked, so that in case
they become loose on the road they can easily be set
again. It is usual, too, to mark the position of the
valves with centre-punch marks on the valve-stem and
on the stuffing-box of the steam-chest, so that with a
gauge made for the purpose the position of the valve
can be determined without taking off the steam-chest
cover.
In some cases the eccentrics are keyed on, which is
done after their position is determined by setting the
valves. The ends of the set-screws which are used to
fasten the eccentrics should be cup-shaped and case-hardened,
so as to hold as securely as possible to the
axle when they are screwed down.
PART XII. THE RUNNING GEAR.
Question 246.What is meant by the running gear of
a locomotive?
Answer. It means those parts, such as the wheels,
axles and frames, which carry the other parts of the
engine. As the Germans express it, it is the “wagon”
of the locomotive.
Question 247.How may the wheels be classified?
Answer. As driving and carrying or truck wheels.
Question 248.What service must the driving wheels
perform?
Answer. The driving wheels, as indicated by their
name, “drive” or move the locomotive on the track,
as was explained in answer to Questions 64, 65 and
66. As their adhesion depends upon the pressure
with which they bear upon the rails, they must carry
either a part or the whole of the weight of the engine.
Question 249.What proportion of the weight of ordinary
locomotives is usually carried on the driving
wheels?
Answer. Eight-wheeled “American” locomotives,
which are most commonly used in this country, have
about two-thirds of their weight on the driving wheels.
Question 250.What is meant by the “truck” of a
locomotive?
Answer. It means one or more pairs of wheels which
are attached to a separate frame and to the locomotive
by a flexible connection, so that the axles are not held
rigidly at right angles to the main frame, but can assume
positions which approximate to that of radii of
the curves of the track. In plates I, II and III, E E
are the truck wheels, b′ b′ the truck frame, and y, plate
II, and fig. 40, the centre-pin, around which the truck
frame turns.
Question 251.What service does the truck perform?
Answer. It carries the weight of the front end of the
locomotive, and also guides it into and around curves
and switches.[67]
[67] A switch is a movable pair of rails, by which a locomotive is enabled
to run from one track to another.
Question 252.How does it perform the latter service?
Answer. It does it very much in the same way as
the front wheels of an ordinary wagon enable it to
turn around corners; that is, the truck wheels being attached
to a separate frame, which is connected to the
locomotive by a centre-pin, just as the front axle of
an ordinary wagon is connected by the king-bolt, can
turn.
Fig. 149.
Fig. 150.
Scale, ³⁄₈ inch = 1 foot.
Fig. 151.
Question 253.Why are two pairs of wheels used on
a locomotive instead of one, as on an ordinary wagon?
Answer. Because it is necessary to have one pair of
wheels guide the other. In an ordinary wagon the
front axle is guided by the pole or shafts. Nearly
every one knows the difficulty of moving a wagon
when the pole or shafts are removed, especially if it be
pushed from behind. The movement of the front
axle is then uncontrolled, and it is impossible to direct
the motion of the vehicle. The same thing would occur
with a locomotive if a single pair of wheels were
used, and attached in the same way as the front axle
of a wagon. Thus if a single pair of wheels were connected
to a locomotive by a centre-pin, a, fig. 149, so
that the axle would be free to move around this pin,
then if one of the wheels should strike an obstruction,
say a stone, s, fig. 150, there would be nothing to prevent
the axle from being thrown into the position shown in
fig. 150, and the wheels would be quite sure to leave
the track. When two pairs of wheels are used and
both axles attached to the same frame, which is connected
to the engine by a centre-pin, s, fig. 151, between
the two axles, then the wheels in moving round the
centre-pin must move around the centre s in arcs of
circles, m n, m n, described from the centre s. These
arcs, it will be observed, cross the rails. Now if the
wheels should move in that direction, the flange of one
of them would come in contact with the rail and prevent
it from moving any farther. It is therefore
evident that wheels arranged in that way can only
move about the centre-pin as far as the curvature of
the track will permit. Trucks are sometimes used
with only one pair of wheels, but the centre-pin is
then placed some distance behind the centre of the
axle, or in the same relation to it that the centre s is
to the axle a a′ in fig. 151. It is evident that if the
frame for such a truck turns around the centre-pin,
the wheels must move across the track in the same
way as represented by the arcs m n, in fig. 151. The
construction and operation of trucks with a single
pair of wheels will be more fully explained hereafter.
Fig. 152.
Fig. 153. Scale
³⁄₁₆ Inch = 1 Foot.
Fig. 154.
Fig. 155.
Fig. 156.
Question 254.Why will a locomotive run around
curves easier if the front axles are attached to a truck
frame which is connected to the locomotive by a flexible
connection?
Answer. Because the truck axles can then assume
positions which conform very nearly to the radii of the
curves of the track, and it is well known that if two
or more axles, each with a pair of wheels on it, are
attached to a frame with their centre lines parallel
with each other, as shown in fig. 152, they will roll in
a straight line, but if the centre lines of the axles are
inclined to each other, as shown in fig. 153, the tendency
will be to roll in a curve, the radius of which
will depend upon the degree of inclination of the axles
to each other. In order to make the wheels in fig.
152 roll on the curves a b and c d, it will be necessary
to slide them laterally a distance equal to that between
the curves and the straight lines m o and p r,
and as the length of the outside curve is greater than
the inside one, if the wheels are fastened to the axles
so they cannot turn on them and roll on the curves,
either the wheels on the inside or those on the outside
must slip a distance equal to the difference in the
length of the two curves. Considerable force will
therefore be required to overcome the resistance due
to the combined lateral and circumferential sliding
of the wheels, so that more power will be needed to
make them roll in a curve than is necessary to make
them roll in a straight line. If, however, the axles
are inclined to each other, then the wheels will naturally
roll on a curved path, and it will not be necessary
to slide them sideways to make them conform
to such a path. But if the wheels are all attached
to the axles so that those on the same axle
cannot turn independently of each other and are all of
the same diameter, then either the inside or the
outside ones must slip, because the path in which
the outside ones roll is longer than the inside curve,
so that even if the axles are inclined to each other
more power will be needed to roll the truck in a
curved path than to roll the wheels shown in fig. 152
in a straight line. It is, however, a fact that a cone
or a portion of a cone like that shown in fig. 154 will
of itself roll on a curve. It will do the same thing if
the middle is cut away, as indicated by the dotted
lines in fig. 154 and as shown in fig. 155. If now the
wheels are made so that their peripheries[68] form portions
of a cone and the axles are inclined to each other
as shown in fig. 156, then there will be no slipping on
the track, because the outside wheel, being larger in
diameter than the inside one, advances further in one
revolution than the latter does, and thus rolls on the
longest path in the same time that the inside or
smaller wheel does on the shorter one. When this is
the case, such wheels will roll in a curve as easily as
those in fig. 152 will in a straight line. The degree of
inclination of the axles and of the sides of the cone
must, however, vary with the radius of the curve. But
if the axles are parallel to each other, and the wheels
conical, as represented in fig. 157, they will not
roll
either in a straight line or in a curve without great difficulty,
because if they roll in a straight line, the wheels
on one side being larger in diameter than those on the
other, either the larger or the smaller ones must slip on
the path in which they roll. If they roll on a curve,
then each pair of wheels has a tendency to roll in a
curve independent of the other, and therefore the wheels
must slip laterally if both pairs roll on the same track.
Thus, suppose two pairs of wheels, a, a′, and b, b′, fig.
157, to be made conical and attached to a frame so that
their axles are parallel to each other. Now each pair
of such wheels will have a tendency to roll in circular
paths, a′ i, a h, and b′ k, b j, the centres of which are
at m and n, or at the apices of the cones of which their
peripheries form a part. If they are made to roll in
circular paths, c d, e f, described from a point g, then
each pair of wheels must slip laterally over the space
between the paths a′ i, a h, in which they would
naturally roll and that in which they are made to roll.
Thus the wheel a would slide laterally the distance
between the curve a h and a f, and a′ that between a′ i
and c d; b would slide from b j to b f and b′ from b′ k
to b′ d. It will thus be seen that in order that two
pairs of wheels may roll with equal ease in a straight
line and in curves, the wheels in the one case must be
of equal diameters and the axles parallel, and in the
other case the wheels must be of unequal diameters
and their axles be radial[69] to the curve. This is equally
true of any number of pairs of wheels. If we have
three, four, or any number of axles, with wheels all
attached to the same frame, if their axles are parallel,
and the wheels of the same diameter, they will roll in
a straight line; but if their wheels are conical and
their axles radial, they will roll in a curve.
[68] The periphery is the outside surface on which the wheel rolls. This
part of a wheel is usually called the “tread.”
[69] That is, that their centre lines incline towards each other, and if extended
far enough would meet at the centre of the curve.
Fig. 157.
Scale ³⁄₁₆ In. = 1 Foot.
For the preceding reasons it is therefore sufficiently
obvious that if a locomotive is to run on both straight
and curved tracks, on the former the wheels should be
of the same diameter and the axles parallel, and on the
latter the wheels should be conical and the axles radial.
Fig. 158.
Fig. 159.
Scale ³⁄₈ in. = 1 foot.
Question 255.How are the wheels made so that in
curves they will act as though they were of the conical form
described and on a straight track all be of the same diameters?
Answer. The periphery or tread of each wheel is
made conical, but of the same size as the other, and
with the small diameter of the cone outside, as shown
in fig. 158. On a straight track if the position of the
wheels on the rails is such that their two flanges are
equally distant from the rails, as shown, then obviously
at the points of contact with the rails the wheels
are of the same diameter. That is, a is equal to b.
But in running on a curved track, if the wheels are of
the same diameter, as has been shown, they will roll
in a straight line and consequently towards the outside
of the curve. The flange c—supposing it to be at
the outside of the curve—will therefore roll towards the
rail, and consequently the outside wheel will rest on
the rail at a point nearer the flange, as shown in fig.
159, where the diameter a is larger, and the inside
one further from the flange where the diameter b is
smaller than at a and b in fig. 158; and consequently
the action of the wheels is the same as though their
peripheries were made of the form shown in fig. 157.
Question 256.How are the axles of locomotives made
to assume a position radial to the curves in the track?
Answer. This is only done approximately, as the
mechanical difficulties in the way of doing it perfectly
are so great as to render it impracticable. By attaching
the truck to the locomotive by a flexible connection
or centre-pin, s, as shown in fig. 160 (which represents
a plan of the wheels of an ordinary locomotive),
it is plain that the truck axles e f and g h, instead of
remaining parallel to the driving-axles a b and c d,
will, by turning around the centre-pin, s, adjust themselves
to the curve so as to approximate as closely to
radii as is possible for two axles which are held parallel
to each other. Of course the further apart they
are the greater will be their divergence from the position
of radii, and whether the tread of the wheels be
cylindrical or conical the further apart their axles are
the greater will be the divergence of the paths in
which they would naturally roll from that of any curve
on which they must roll. Thus, if the axles were
twice as far apart as they are represented in fig. 157,
and in the position shown in the dotted lines l l′ and
o o′, the wheels, if they are conical, would then naturally
roll in curves drawn from the centres p and q.
If the wheels are cylindrical, they would roll in
straight lines. In either case the divergence of their
paths l s and l r from the curve of the track is greater
than a h and a′ i, the paths in which they would roll if
their axles were nearer together. This divergence increases
with the distance between the axles, and therefore
the lateral slip of the wheels must be in the same
proportion.
Fig. 160. Scale ³⁄₁₆ Inch — 1 Foot.
Question 257.Is the resistance to rolling diminished
by placing the truck axles nearer together?
Answer. It is, within certain limits. The nearer
each other they are placed, the closer will the centre-pin
of the truck be to the centre of the axles. The closer
it is to the centre of the axle, the greater is the tendency
of the wheels to become “slewed,” or to assume
a diagonal position to the rails as represented in fig. 150,
and thus increase the resistance and also the danger
of running off the track. The increase of resistance
from this cause, after the axles reach a certain distance
from each other, is greater than the decrease
from a closer approximation to the position of radii.
In ordinary locomotives it is necessary to place the
truck wheels from 5 ft. 6 in. to 6 ft. apart, in order to
get the cylinders between them in a horizontal position.
This distance apart works very well in ordinary
practice.
Question 258.What is meant by flange friction?
Answer. It is the friction of the flanges of the wheels
against the head of the rails. Thus if two pairs of
wheels, a a′, b b′, fig. 151, be placed on a curve and
rolled in the direction of the dart, the wheel a will roll
towards the outside of the curve until the flange comes
in contact with the rail. As already explained, if two
axles are parallel to each other, no matter whether the
wheels are conical or cylindrical, they must slip laterally
in order to roll in a curved path. As the flange
must follow the curve of the rail, it forces the wheel
laterally and thus compels it to roll in the curved
path into which the rail is bent. As the wheel offers
considerable resistance to sliding there is a corresponding
pressure of the flange against the rail, and
consequently the revolutions of the wheel produce an
abrasive action between the two. This action is obviously
increased with the distance between the axles,
because, as has been shown, the lateral slip of the
wheels is then greater than when they are nearer together.
It is also obvious that if the wheels are parallel
with the rails there will be no abrasive action of
the flanges, but that the greater the angle at which
the wheels stand to the rails the harder will the flanges
rub against the rails, and the greater will be the
flange friction. With the aid of geometry it can very
easily be proved that the farther apart two parallel
axles are, the greater will be the angle of the wheels
to the rails on a curved track, and, therefore, the
greater will be their flange friction. It must, however,
be remembered that if the wheels are so close together
that they are liable to become “slewed,” or assume a
diagonal position across the rails, as shown in fig. 150,
the angle at which the wheels would stand to the rails
would thus be very much increased. It has therefore
come to be a very generally recognized rule that the centres
of axles should never be placed nearer together
than the distance between the rails.
Question 259.Is the flange friction of all the wheels
of a truck the same on any given curve?
Answer. No; of the front wheels obviously only the
flange of the one on the outside of the curve comes in
contact with the rail. As the centrifugal force of the
engine presses the back pair of wheels towards the
outside of the curve, the flange of the outside wheel
alone comes in contact with the rail. But as this
wheel is constantly rolling away from the rail, as
shown by the dotted lines h g, fig. 151, obviously the
friction of its flange is less than that of the front outside
wheel, which always rolls towards the rail. The
flange of the back inside wheel is carried outwards by
the centrifugal force and also by the tendency of the
wheels to roll on their largest diameters on a curve, so
that its flange will not touch the rail.
Question 260.Can the axles of driving wheels assume
positions radial to the track?
Answer. In ordinary engines they cannot. Various
plans have been devised for the purpose of enabling
them to do so, but it is only recently that they have
met with any success. Some of these plans will
be described hereafter. It is, however, of less importance
that the driving axles, when they are behind
the centre of the locomotive, should assume positions
radial to a curved track than that the front wheels
should. This is illustrated by a common road wagon,
as all know the ease with which such a vehicle can
turn a corner if we run it with the front axle ahead,
and the difficulty of doing so when the back axle is in
front. In the case of a locomotive the reason for it is
very much the same as that which makes the flange
friction of the back wheels of a truck less than that of
the front ones. From fig. 160 it will be seen that the
outside driving-wheels, when the engine is running
with the truck in front, are rolling from the rail and
not against it. As stated before, the centrifugal
force of the engine when in motion has a tendency
to throw the wheels towards the outside of
the curve. It will also be noticed that the front
driving axle is near the centre of that portion of the
curve which lies between the centre s of the truck and
the centre k of the back axle. If it were in the middle
between them, it would be exactly radial to the
curve; being near the middle, it approximates closely
to that position, and therefore the flange friction of
its wheels is very slight. It will be noticed that if
the flange of the back or trailing-wheel on the inside
of the curve were not kept away from the rail it would
roll toward and impinge against that rail. But it will
be noticed that the flange of the front driving-wheel
will come in contact with the inside rail before that
on the back wheel can touch it. For this reason, and
also on account of the effect of the centrifugal force
exerted on the engine and the tendency of the wheels
to roll on their largest diameters, the flange of the inside
back wheel is kept out of contact with the rail,
and as the back wheel on the outside of the curve
rolls away from the rail there is very little friction of
the flanges of the back driving-wheels.
It will also be noticed from fig. 160, that if the radius
of the curve is very short, the bend of the rails
between the back pair of driving-wheels and the centre
of the truck is so great that the inside rail will
press hard against the flange of the front or main
driving-wheel next that rail. This of course produces
a great deal of friction, and if the curve is excessively
short the flange will mount on top of the rail and the
tread of the opposite wheel will fall off from its rail.
For this reason the centre-pin of the truck is sometimes
arranged so that it can move laterally, that is
cross-wise of the track. In fig. 160 the centre-pin is
represented as having moved some distance from the
actual centre of the truck, which is represented with
dotted lines. The front wheels of locomotives are also
sometimes made with wide “flat” tires, that is, tires
without flanges, so that there will be no friction
against the one rail and no danger of falling off the
other.
Another action also takes place which facilitates
the motion of the driving-wheels of ordinary engines
around curves. Every one knows how easy the direction
in which the front wheels of a common wagon
can be controlled by taking hold of the end of the
tongue or pole. With the leverage which it gives the
wheels and axle can easily be directed wherever it is
desired. A similar action takes place in an ordinary
locomotive. The front driving-axles are guided by
the truck, which is attached to the frame ten or twelve
feet in front of the driving-axle, and thus the track
exerts a leverage to guide the movement of the
driving-axles, just as a common wagon can be guided
by the pole.
If the locomotive is run backward, then none of
these advantages exist, and the flange friction of the
back driving-wheels is excessive. Engines such as
construction locomotives, which run backward as much
as forward, wear out the flanges of the back wheels
very rapidly on crooked roads.
Question 261.What is meant by the “spread” of the
wheels or axles?
Answer. It is the distance between the centres of
two axles.
Question 262.What is the “wheel-base” of a locomotive?
Answer. It is the distance between the centres of the
front and back or trailing-wheels. On ordinary engines,
such as that illustrated in plate I, it is the distance
from the centre of the front truck to the centre
of the back driving-wheels.
Question 263.Is the “coning” of the tread of the
wheels of much practical importance?
Answer. There is great difference of opinion regarding
it, but even if its action is very beneficial, the advantage
is very soon lost, owing to the wear of the
wheels. It is, therefore, believed that the advantage
is more apparent in theory than in practice.
Question 264.How are the driving-wheels of locomotives
constructed?
Answer. They are made of cast iron with wrought-iron
or steel tires around the outside. Fig. 161 represents
a perspective view of a pair of locomotive wheels
and axle. The central portion of the wheel, that is
the hub, spokes and rim, are cast in one piece. Usually
the hub and the rim, and sometimes the spokes,
are cast hollow. The central portion of the wheel,
that is the part which is made of cast iron, is called
the wheel-centre.
Fig. 161.
Question 265.How are the tires fastened on the
wheel-centres?
Answer. The insides of the tires are usually turned
out somewhat smaller than the outside of the wheel-centre.
The tire is then heated so that it will expand
enough to go on the centre. It is then cooled off, and
the contraction of the metal binds it firmly around the
cast iron part of the wheel. As an additional security
bolts or set-screws, a, a, fig. 161, are screwed through
the rim and into the tire to prevent it from slipping
off in case it becomes loose. In some cases the wheel-centre
and the inside of the tire are turned conical,
and the tires are then put on cold and held on with
hook-headed bolts, C, as shown in fig. 162, which is a
section of the tire and the rim of the wheel. The
wheel-centre is made largest on the inside. As the
strain against the flange of the tire is inward, the
cone of the wheel-centre resists this strain. If it was
curved or tapered the reverse way, the strain would
come on the bolts, and it would also be impossible to
remove the tires without first taking the wheels off
the axles. This method of putting on tires has the
advantage that they can be removed quickly and without
heating the tires.[70]
[70] It is exclusively used on the Baltimore and Ohio Railroad.
Fig. 162. Scale 3 in. = 1 foot.
Question 266.Are there any standard sizes for the
inside diameters of tires?
Answer. Yes. To avoid the great inconvenience
arising from the diversity in the inside diameters of tires,
the American Railway Master Mechanics’ Association
has recommended that the inside diameter of tires should
be made 36, 40, 44, 50, 56 and 62 inches. The thickness
for the first three sizes to be 3 in. and the last
three 2¹⁄₂ in.
Question 267.How are the driving-wheels fastened
on the axles?
Answer. The hubs are accurately bored out to receive
the axles, and the latter are turned off so as to
fit the hole bored in the wheel. The axles are then
forced into the wheel by a powerful pressure produced
either with a hydraulic or screw press, made for the
purpose. In order to prevent the strain upon the
crank-pins from turning the wheels upon the axle,
they are keyed fast with square keys driven into
grooves cut in the axle and in the wheel to receive
them. The ends of these keys are shown at b, fig.
161.
Question 268.How are the crank-pins made?
Answer. They are made of wrought iron or steel
and accurately turned to the size required for the journals
for the connecting-rods. Fig. 164 represents one
of the main crank-pins, and fig. 163 a back pin for an
American engine. The main pin has two journals,
one, B, to which the main connecting-rod is attached,
and the other, A, receiving the coupling-rod. The
back pin has only one journal, A, for the coupling-rod.
Question 269.How are the crank-pins fastened to the
wheels?
Answer. They are turned so as to fit accurately
holes which are bored in the wheels, and are usually
“straight” or cylindrical. The pins are then either
driven in with blows from a heavy weight swung from
the end of a rope, or else pressed in with a screw or hydraulic
press. Sometimes the holes are bored tapered
or conical and the pins turned to the same form.
They are then ground in with emery and oil, so as to
fit perfectly, and are secured by a large nut and key
on the inside of the wheel.
Fig. 163.
Fig. 164.
Scale 1¹⁄₂ in. = 1 foot.
Question 270.What are the pieces A, A, fig. 161, between
the spokes of the wheel for?
Answer. They are called counterbalance weights, and
are put in the wheels to balance the weight of the
crank-pins, connecting-rods and pistons. The principle
of their action will be explained hereafter.
Question 271.On what part of the axle does the
weight of the engine rest?
Answer. It rests on the driving-axle boxes L, fig. 161,
which are placed just inside and close to the wheel.
Fig. 165.
Question 272.What are the driving-axle boxes for
and how are they made?
Answer. They are cast iron blocks, L, fig. 161, which
embrace and rest on the axle. The part of the axle
on which the box bears is called the journal. Each
box has a brass bearing, c, fig. 165, which bears on top
of the journal and which is consequently exposed to
the friction and wear. Fig. 165 is a perspective view
of a driving-box, which shows what is called the oil-cellar,
d. This is a receptacle underneath the axle
which is filled with wool or cotton waste and saturated
with oil for the purpose of lubricating the journal.
The oil-cellar is held in its position by two bolts, f, f,
which pass through it and the driving-box casting.
By removing the bolts the oil-cellar can easily be removed
and the box can then be taken off the axle.
Fig. 166.
Fig. 167.
Scale ¹⁄₂ in. = 1 foot.
Question 273.How are the truck wheels made?
Answer. They are made of cast iron, usually in one
piece. Figs. 166 and 167 represent sections of two
forms of wheels used for cars. Those used for locomotive
trucks are similar to these, excepting that they
are usually a little smaller in diameter. They are
made with a disc or plate which unites the tire to the
hub, and in some cases they have ribs cast in the inside,
as shown in the two figures. Some are made
with single and others with double plates, as shown in
the engravings, and still others with spokes similar to
the driving-wheels. The tread of the wheel is hardened
by a process called chilling. This is done by
pouring the melted cast iron into a mould of the form
of the tread of the wheel. The mould is also made of
cast iron, but being cold cools the melted iron very
suddenly, and thus hardens it somewhat as steel is
hardened when it is heated and plunged into cold
water.[71]
[71] It should be mentioned here that it is only certain kinds of cast iron
which will be hardened in this way, or will “chill,” as it is called. The
cause to which this chilling property is due is not known.
Question 274.How are the boxes, journals and journal-bearings
of the truck-wheels made?
Answer. They are very similar to those for the driving-wheels,
their chief difference being that those for
the truck-wheels are smaller than those for the driving-wheels.
Question 275.How are the frames for locomotives
constructed?
Answer. The frames, H H H, plates I,
II and III,
are made of bars of wrought iron from 3 to 4 inches
thick and about the same in width. They are usually
made in two parts, the one at the back part of the engine,
to which the driving-boxes and axles are attached,
and the other at the front end, to which the
cylinders are bolted. The back part, or main frame,
as it is called, is represented in figs. 168 and 169, and
consists of a top bar, H H, to which pieces, a, a′, b, b′,
called frame-legs, are welded. Two of these form what
is called a jaw, which receives the axle-box, as shown
in fig. 169. To the bottom of each jaw a clamp, c, is
bolted to hold the two legs together. The two legs, a
and b′, are united by a brace, d d, welded to the bottom
of the legs. A brace, m, unites the back end of
the frame with the leg b, and is welded to each.
The front part of each frame consists of a single
bar, e, which is bolted to the back end, as represented
in figs. 168 and 169, which show the construction
clearer than any description would. These front bars
extend forward to the front end of the engine, and a
heavy timber, called a bumper-timber, E′ E′, plates I, II
and III, extends across from one to the other and is
bolted to each of them. This timber is intended to
receive the shock or blow when the locomotive runs
against any object, such as a car. The cow-catcher or
pilot, S, is fastened to this timber.
Fig. 168.
Fig. 169.
Scale ³⁄₈ in. = 1 foot.
The front bar of the frames also has usually two
lugs or projections forged on it, between which the
cylinders are attached. The latter are securely held
in their position by wedges, which are driven in between
the lugs and the cylinder castings.
The frames, as already stated, are made of wrought
iron and are accurately planed off over their whole
surface.
Question 276.How are the frames fastened to the
boiler?
Answer. As already stated, they are fastened to the
cylinders with wedges and bolts, and as the cylinders
are bolted to the smoke-box the frames are thus rigidly
attached to the front end of the boiler. In order to
strengthen those portions of the frames which extend
beyond the front of the smoke-box and to which the
bumper-timber is attached, diagonal braces, r′ r′, plates
I, II and III are bolted both to the timber and to each
of the frames at their lower ends. The upper ends are
bolted to the smoke-box. Other braces, d′, plate II,
are also fastened to the frames and to the barrel of the
boiler. The frames are fastened to the fire-box by
clamps, I, I, plate I, called expansion clamps. These
clamps embrace the frames so that the latter can slide
through the former longitudinally. There are also
usually two diagonal braces not shown in plate II, the
upper ends of which are fastened to the back end of
the shell of the fire-box at about the level of the crown-sheet,
and the lower ends to the back ends of the
frames. There are also usually transverse braces attached
to the lower part of the frames, thus uniting
the two together. The guide-yokes, j j, plate I, are
also usually bolted to the frames and to the boiler. In
many cases one only is used, which extends across
from one frame to the other and is fastened to the
boiler.
Question 277.Why are the frames attached to the
shell of the fire-box so as to slide longitudinally through
the fastenings?
Answer. Because when the boiler becomes heated
it expands, and if it could not move independent of
the frames its expansion would create a great strain
on both itself and the frames. The fastenings to the
fire-box are therefore made so that the frames can
move freely through them lengthwise, but in no other
direction.
Question 278.How much more will the boiler expand
than the frames in getting up steam?
Answer. From ¹⁄₄ to ⁵⁄₁₆ of an inch.
Question 279.Why is it necessary to support the
engine on springs?
Answer.[72]Because, however well a road may be
kept up, there will always be shocks in running over
it; these occur at the rail joints and especially when
the ballasting of the ties is not quite perfect. These
shocks affect the wheels first, and by them are transferred
through the axle-boxes to the frame, the engine
and the boiler. The faster the locomotive runs, the
more powerful do they become, and therefore the more
destructive to the engine and road, and consequently
the faster a locomotive has to run the more perfect
should be the arrangement of the springs.
[72] The above answer and much of the material referring to springs has
been translated from “Die Schule des Locomotivführers,” by Messrs.
J. Brosius and R. Koch.
If we strike repeatedly with a hammer on a rail,
the latter is soon destroyed, while it can bear without
damage a much greater weight than the hammer
lying quietly on it. The axles, axle-boxes and wheels
strike like a hammer on the rails at each shock, while
the shock of the rest of the parts of the engine first
reaches and bends the springs, but on the rails has
only the effect of a load greater than usual resting on
them. Another comparison will make still plainer
the lessening by the springs of the injurious effect
which the weight of the boiler, etc., exercises on the
rails.
A light blow with a hammer on a pane of glass is
sufficient to shatter it. If, however, on the pane of
glass is laid some elastic substance, such as india-rubber,
and we strike on that, the force of the blow
or the weight of the hammer must be considerably
increased before producing the above-named effect.
If the locomotive boiler is put in place of the hammer,
the springs in place of the india-rubber, and the
rails in place of the glass, the comparison will agree
with the case above. From this consideration it will
be seen how important it is to make the weights of
the axles, axle-boxes and wheels as light as possible.
Question 280.How are the driving-axle boxes
arranged so that the weight of the engine will rest on
springs?
Answer. They are arranged so as to slide up and
down in the jaws. Springs, B, B′, fig. 169, are then
placed over the axle-boxes and above the frames.
These springs rest on ∩-shaped saddles, G′, G′, which
bear on the top of the axle-boxes. The frames are
suspended to the ends of the springs by rods or bars,
g, g′, g, g′, called spring-hangers. As the boiler and
most of the other parts of the engine are fastened to
the frames, their weight is suspended on the ends of
the springs, which, being flexible, yield to the weight
which they bear.
Question 281.How are the frames protected from
the wear of the axle-boxes which results from their sliding
up and down in the jaws?
Answer. The insides of the legs, a, a′, b, b′, are protected
with shoes or wedges, h, h, which are held stationary,
and the box slides against the faces of the
shoes, thus wearing the shoe or wedge but not the
frame.
Question 282.Why are the shoes usually made wedge-shaped?
Answer. They are made in that way so that when
they become worn, by moving one or both of them up
in the jaws, the space between them is narrowed and
the lost motion is taken up. They are moved by the
screws i, i. If the boxes should become loose from
wear, it would cause the engine to thump at each revolution
of the wheels or stroke of the piston.
Question 283.How are the springs for the driving-wheels
made?
Answer. They are made of steel plates which are
placed one on top of the other. These plates are of
different lengths, as shown at B, B′, in fig. 169, and
are from 3 to 4 in. wide and ⁵⁄₁₆ to ⁷⁄₁₆ thick. The
length of the springs measured from the centre of one
hanger to the centre of the other is usually about three
feet.
Fig. 170.
Fig. 171.
Question 284.What determines the amount which a
spring will bend under a given load?
Answer. The number of plates, their thickness,
length and breadth, and of course the material of
which they are made. This can be explained if we
suppose we have a spring plate of a uniform thickness,
h, and a triangular form, of which fig. 170 is a
side view and 171 a plan, and that it is clamped fast
at its base, b. It is a well known mechanical law
that any material of this form and under these conditions
will have a uniform strength through its whole
length to support any load, P, suspended at its end,
and also that it will bend or deflect in the form of an
arc of a circle.
Fig. 172.
Fig. 173.
Fig. 174.
Fig. 175.
Scale ³⁄₄ in. = 1 foot.
Question 285.How are locomotive springs usually
made?
Answer. In locomotives the arrangement of springs
is always such that they are either supported in the
middle and moved at the two ends, or such that they
are supported at the two ends and loaded in the middle;
for our consideration it is indifferent which of the
two kinds of springs is taken for the present illustration.
That shown in plan and elevation in figs. 172
and 173, which is formed of a wide plate placed diagonally,
and which in reality consists of two such triangular
pieces as were represented in fig. 171 united
at their bases m m, and loaded at two opposite corners,
e and f, would answer the requirements mentioned if
the great breadth, m m, were not an obstacle. This
breadth is obviated by cutting the spring into several
strips, a a, b b, c c, d d, ... i, fig. 173, of equal width,
and placing these not side by side, but one over the
other, as shown in figs. 174 and 175.
In order that the separate strips and layers of the
spring so made, figs. 174 and 175, may not slip out of
place, the strips a a, b b, etc., are made in one piece,
and all the plates are inclosed with a strap, F, figs.
176 and 177. The plates, instead of being cut from
a piece like that represented in fig. 173, are, however,
made out of steel of the proper width, and the ends, instead
of being cut off pointed as represented, are sometimes
drawn out thinner on the ends, like the point of a
chisel, or oftener still cut off straight, as shown in fig.
177.
Fig. 176.
Fig. 177.
Fig. 178.
Scale ³⁄₄ in. = 1 foot.
In order to hold the plates together a band, F, is
put around the middle. This is put on hot, and becomes
tight by contracting as it cools. The centre of
the spring has a hole drilled through it with a pin, s,
fig. 178 (which shows a cross section of a spring), to
prevent the plates from sliding endwise. The plates
at each end usually have a depression, a, fig. 179
(which is a cross section of a plate on a larger scale
than the preceding figure), made in them on one side,
and a corresponding elevation, b, on the other. The
elevation on one plate fits into the depression on the
other, and thus prevents the plates from slipping sideways.
Fig. 179.
Scale 6 in. = 1 foot.
Fig. 180.
Scale ³⁄₄ in. = 1 foot.
Question 286.How should springs be curved?
Answer. Springs should be curved so that when
they bear the greatest load which they must carry
they will be straight. If they are curved too much
they are subjected not only to a strain which bends
the plates, but to one which has a tendency to compress
them endwise. Thus if a spring like that represented
in fig. 180 is bent into a half-circle, it is obvious
that the strain at the ends has no tendency at
all to bend the plates, but only to compress them endwise.
Near the middle the strain will of course bend the
spring. In the one direction the spring is flexible and
elastic, and in the other it is not; and as the strain
of compression depends on the amount of curvature,
the greater the latter is, the less flexibility and elasticity
the spring will have.
Springs are often given a double curve, as shown in
fig. 181. This is not to be recommended, because
when a spring bends the plates must slide on each
other. If they have but a single curve, they will
do so and remain in contact through their whole
length, but if they have two curves they will separate
and therefore “gape,” as it is called.
Fig. 181.
Scale ³⁄₄ in. = 1 foot.
Question 287.What is meant by the elasticity of a
spring?
Answer. It is the amount which a spring will deflect
or bend under a given load without having its form
permanently changed. If the bending is so great that
the spring does not recover its original form when the
load is removed, then the strain to which it is subjected
is said to exceed the limits of elasticity, and if repeated
often it will ultimately break the spring.
Question 288.What is meant by the elastic strength
and the ultimate strength of a spring?
Answer. The elastic strength is the strain it will bear
without being strained beyond the limits of elasticity,
and the ultimate strength is the strain which will break
it.
Question 289.What determines the strength of a
spring?
Answer. It depends of course (1) upon the material
of which the spring is made; (2) its strength increases
in proportion to the number of plates, and (3) to their
width, and (4) in proportion to the square of their
thickness, and (5) as the length diminishes.
Thus, if we wanted to double the strength of a
spring like that shown in figs. 170 and 171, it could be
done in either of the following ways: (1) by making
it of material twice as strong; (2) by putting another
plate just like it on top; (3) by doubling the width of
the base b, which would make the strength of the
whole plate twice what it was before; (4) by making
the whole plate about four-tenths thicker, which
would increase its strength, as already stated, in proportion
to the square of the thickness as 1.4 × 1.4 = 2
nearly; (5) by reducing the length to one-half what
it is in fig. 170.
Question 290.What determines the elasticity of a
spring?
Answer. (1) The material of which it is made; with
the same material the elasticity increases (2) as the
number, and (3) as the width of the plates diminishes,
and (4) with the cube of the length, and (5) decreases
with the cube of the thickness of plate.
Thus, supposing the plate in figs. 170 and 171 to
be ³⁄₈ in. thick and the deflection d 2¹⁄₂ in.; the latter
would be only half as much or 1¹⁄₄ in. (1) if it were
made of material twice as stiff, or (2) with two such
plates, or (3) with one twice as wide at the base. If (4)
the length were doubled, the deflection would be equal
to 2 × 2 × 2 = 8 times what it was before, or in proportion
to the cube of the length. If (5) the thickness
were doubled the deflection would be reduced in the
same proportion, and would be only one-eighth of 2¹⁄₂
in., or ⁵⁄₁₆ in.
Fig. 182.
Fig. 183.
Scale ³⁄₄ in. = 1 foot.
Question 291.What should be the proportion of the
plates of a spring in relation to each other?
Answer. The lower plates should diminish regularly
in their lengths. The reason for this will be apparent
from the fact which has already been stated, that if a
triangular plate of uniform thickness is clamped fast
at its base, it will, if loaded at the end, be of uniform
strength throughout its whole length. It is immaterial
what the length of the base of such a triangle is,
if the two sides are of equal length and the thickness
of the plate is uniform, not only its strength but the
amount of deflection or bending from any load will be
equal all through its length. If, therefore, we make
a spring by cutting a plate formed of two such triangular
pieces united at their bases into strips, as has
already been explained, evidently the spring made of
them will have a uniform strength throughout its
whole length. As the strips thus made diminish in
length regularly, it is evident that if the spring
plates are made of steel rolled of the requisite width,
their length should be the same as that of those cut
from the plate referred to above. When this is the
case the lower outline, a b b a, fig. 183, of the spring
will, when the spring is not bent, be straight lines.
Sometimes the lower outline of springs is made curved,
as shown in fig. 182. This gives too much strength
near the strap F, and too little near the ends. In
drawing springs, therefore, it is best to lay them out
with the plates straight, as shown in figs. 182 and 183,
and after determining the thickness, drawing a straight
line from the strap to the end of the longest plate will
give the best form of the spring and the length of each
of the plates. It is necessary, however, to put a sufficient
number of long plates in each spring to give it
the required strength next to the attachment of the
hanger. Sometimes one or more of these long plates
are made heavier than the rest. The evil of this
method of construction will be apparent if it is remembered
that the greatest permissible deflection up to
the breaking of the spring decreases with the cube of
the thickness of the plate and its strength increases
with the square of the thickness. Now if we have a
spring with say ten plates ³⁄₈ in. thick and one on top ³⁄₄
in. thick, the thick plate will have a strength four
times that of the thin plates, but its elasticity will be
only one-eighth that of the thin plates, and therefore
it will require eight times as much load to bend it any
given distance as is needed to bend the thinner plates
the same distance. But its strength is only four times
that of the thin plates, so that for any given amount
of elasticity the thick plate must bear twice as much
load as it has strength to carry. This shows what a
great mistake is committed if some of the plates are
made thicker than others, a conclusion which is supported
by practical experience, as it is found that if
the top plates are made thicker than others, the thick
ones break most frequently, which is the necessary result
of the supposed strengthening by increasing the
thickness of the top plates.
Question 292.[73]How can we find by calculation the
elasticity or deflection of a given steel spring?
[73] The following rules for calculating the proportion and strength of
steel springs are from Clark’s Railway Machinery.
Answer.By multiplying the breadth of the
plates in inches by the cube of the thickness
in sixteenths, and by the number of plates:
divide the cube of the span[74]in inches by the
product so found, and multiply by 1.66. The
result is the elasticity in sixteenths of an
inch per ton of load.
[74] The span is the distance between the centres of the spring-hangers
when the spring is loaded.
Question 293.How can we find the span due to a
given elasticity and number and size of plates?
Answer.By multiplying the elasticity in sixteenths
per ton by the breadth of plate in
inches, and by the cube of the thickness in
sixteenths, and by the number of plates: divide
by 1.66, and find the cube root of the
quotient. The result is the span in inches.
Question 294.How can we find the number of plates
due to a given elasticity, span, and size of plate?
Answer.By multiplying the cube of the span
in inches by 1.66; then multiplying the elasticity
in sixteenths by the breadth of plate
in inches, and by the cube of the thickness in
sixteenths: divide the former product by the
latter. The quotient is the number of plates.
Question 295.How can we find the working strength,
that is the greatest weight it should bear in practice, of a
given steel-plate spring?
Answer. By multiplying the breadth of plates
in inches by the square of the thickness in sixteenths,
and by the number of plates; multiply,
also, the working span in inches by 11.3:
divide the former product by the latter. The
result is the working strength in tons (of 2,240
pounds) burden.
Question 296.How can we find the span due to a given
strength, and number and size of plate?
Answer. By multiplying the breadth of plate
in inches by the square of the thickness in
sixteenths, and by the number of plates; multiply,
also, the strength in tons by 11.3: divide
the former product by the latter. The
result is the working span in inches.
Question 297.How can we find the number of plates
due to a given strength, span and size of plates?
Answer. By multiplying the strength in tons
by the span in inches, and by 11.3; multiply
also, the breadth of plate in inches by the
square of the thickness in sixteenths: divide
the former product by the latter. The result
is the number of plates.
Question 298.How can we find the required amount
of curvature or set of the spring before it is loaded?
Answer.By multiplying the elasticity, per
ton, in inches, by the working strength in
tons; add the product to the desired working
compass. The sum is the whole original set,
to which an allowance of ¹⁄₈ to ³⁄₈ in. should be
added to the permanent setting of the spring.
Question 299.How are the spring-hangers attached
to the ends of the springs?
Answer. A great variety of methods have been used.
The most common ones are those shown in fig. 169.
There the hanger embraces the spring at the ends,
g, g, (shown on an enlarged scale at a, in figs. 176 and
177.) The end of the spring has two projections
forged on its end to receive the upper end of the
hanger, which is made to fit the groove thus formed
between the two projections. The other end, b, of
the spring, figs. 176 and 177, has an eye cut in it
which receives the hanger b. The latter is made of a
single bar, and also has an eye, c, to receive a key
which sustains the weight suspended on the hanger b.
The back end of the front springs and the front end
of the back springs are made in this way because they
come on the side of the fire-box, and if their width
was increased by the thickness of the hanger, as shown
at a in fig. 177, it would rub against and wear the
outer shell of the fire-box.
Question 300.How are the lower ends of the hangers
attached?
Answer. The front hanger, g, fig. 169, of the front
spring, and the back hanger, g, of the back spring
have eyes and pins in their lower ends, k, as shown
in the engraving. The pins are supported by rubber
springs, l, l, which are held between two concave castings,
n, k, one of each of which rests against the
frames. The object of the rubber springs is to relieve
the spring-hangers from sudden shocks and
strains. The benefit derived from their use is believed
to be purely imaginary, as the spring itself, if
sufficiently elastic, should absorb the sudden shocks
which the wheels and axles will convey to the hangers.
Question 301.Why are the ends g′, g′ of the springs
attached to the lever[75]A A?
[75] This lever is called an equalizing lever or beam, or, more briefly, an
equalizer.
Answer. Because if there is a spring for every axle
and the hangers are fastened to the frame, then evidently
the locomotive has as many points of support
as it has axle-boxes. Every shock from the rails is
transferred through the wheel and the axle to the
nearest axle-box and the spring belonging to it, and
the latter must be made strong enough to receive and
dispose of the whole of it. If the adjacent hangers,
g′, g′, fig. 169, of the adjoining springs, B and B′, are
connected by an equalizing lever, A A, which turns
on the fixed point C, then the shock which affects one
wheel will be transferred first to the corresponding
spring. From this spring a part of the shock will be
transferred to the frame by the hanger g, and a part
by the hanger g′ to the equalizer, which will transfer
the pressure to the adjoining spring B′. If by some
unevenness of the road or a powerful oscillation of the
locomotive, a spring is momentarily burdened, the
equalizer thus causes the next wheel to receive part
of this load.
The advantages of this arrangement are evident:
since the springs have to receive only a part of the
shocks, they can be made less strong and therefore
more flexible. The danger of running off the track
and that of breaking axles, springs and hangers, is
therefore reduced by the use of equalizing levers.
Question 302.How are the equalizing levers constructed?
Answer. They are made of wrought iron and are
supported in the centre by a fulcrum, C, which is
fastened to the frame or boiler or both. The spring-hangers
g′, g′ are usually attached to the lever by eyes
and keys. Sometimes eyes are made in the lever, as
shown in fig. 169, and the hanger is inserted into the
eye and held either with a key or else with projections
which are forged on the hanger below the lever. In
other cases the hangers are made with an eye which
embraces the end of the lever.
Question 303.How is the distribution of weight of
the engine affected by the equalizing levers?
Answer. The weight is equally distributed on all
the driving-wheels. This is apparent if it is observed
that the weight suspended from each of the spring-hangers
of each spring in fig. 169 must be the same;
for if the weights in the two hangers, g′ and g′, were
unequal, then the end of the spring which supports
the heaviest weight would be drawn down until the
pressure was equalized. If the weights suspended
from the two hangers, g′ and g′, attached to the equalizing
lever were unequal, then the one supporting the
greatest load would draw up its end of the equalizer
until the weights were again in equilibrium.
Fig. 184.
Fig. 185.
Scale ³⁄₈ in. = 1 foot.
Another effect of the equalizing levers is that each
side of the locomotive is supported in such a way that
the action is the same as it would be if it was supported
on one point. If, for example, we have a
heavy beam, say a piece of timber like that shown by
A B, fig. 184, suspended at one point, C, in its centre,
to the middle, a, of a long spring, D E, the ends
of which rest on two supports, F and G, it is evident
that if the point of suspension is at the middle, C, of
the timber and a of the spring, the weight of the timber
will rest equally on the two supports, F and G, and that
the ends of the timber can move up or down or vibrate
about the point of suspension, C, without affecting the
distribution of weight on the supports, F and G. If,
now, the timber is suspended from three points, A, C
and B, fig. 185, that is, its middle and two ends, as
shown in fig. 185, the ends, A and B, being attached
to the ends of the springs b c and d e, the latter resting
on the supports F and G, and connected at their
opposite ends to an equalizer, f g, whose fulcrum is at
a, it is evident that each of the end hangers must support
one-half of that part of the weight of the timber
between it and the middle, and that the centre hanger
must support one-half the weight between the middle
and the two ends. Thus the hanger A b must support
one-half the weight of the timber between A and
C, and B e must support one-half of that between B
and C; in other words, the end hangers would each
sustain one-fourth of the weight of the timber and
the middle one-half of its weight. If the weight of
the timber is 1,000 pounds, the end hangers would
each sustain 250 and the middle one 500 pounds.
The weight of the middle of the timber is hung on
the equalizer, and one-half, or 250 pounds of it is thus
transferred to each of its ends f and g, and thence to
the hangers f c and g d, and thus to the springs, so
that the ends, c and d, of the springs, sustain a weight
of 250 pounds, therefore, as the opposite ends also sustain
the same weight, it is evident that each of the
springs bears a total load of 500 pounds, or one-half
of the weight of the timber, which is the same load
they sustained in fig. 164. If the ends of a timber
supported as shown in fig. 185 are moved up or down
about the centre point of suspension, it is evident that
the distribution of weight would not be affected any
more than it was in fig. 164 by a similar movement,
because if the ends of the timber move as shown by
the dotted lines around the centre point of suspension
C, the end A will ascend as much as B descends.
The same thing is true of the ends b and e of the
springs and of their opposite ends c and d, and also
of the ends of the equalizer, so that when the timber,
springs and equalizer are in the position shown by the
dotted lines, it is in equilibrium, just as it was when
the timber was horizontal; and therefore the weight
on the supports is the same in both cases, thus showing
that the load A B can move about the centre of
suspension when supported as shown in fig. 185 as
freely as it can if arranged as shown in fig. 184. It
therefore follows that in the distribution of the weight
of each side of the locomotive on the wheels and on
the track, it may be regarded the same as though it
was supported at one point, which is the fulcrum of
the equalizing-lever.
Question 304.What advantage results from supporting
the weight of the back part of the locomotive on two
points?
Answer. If the back part of the locomotive rests on
only two points and the front end on the centre of the
truck, then the whole weight of the engine will be
sustained on three points. Now it is a well known
fact that any tripod, like that on which an engineer’s
level is mounted, or a three-legged stool, will adjust
itself to any surface, however uneven, and stand firmly
in any position; whereas if there are more than three
points of support, if they are all of the same length
the surface on which they rest must be a plane, otherwise
some of them will not touch. All railroad tracks
have inequalities of surface, and therefore it is of the
utmost importance that a locomotive should be able to
adjust itself on its points of support to any unevenness
of the track on which it must run. This is possible
only when the weight rests on three points of support.
Fig. 186.
Fig. 187.
Fig. 188.
Scale, ³⁄₈ inch = 1 foot.
Question 305.How is the truck constructed?
Answer. It consists, as has already been stated, of
two pairs of wheels.[76] These are attached to a frame,
b′ b′, plates I, II and III. The axles have boxes
called truck-boxes, and brass bearings similar to those
used on the driving-axles. These boxes work in jaws,
also similar to those on the main engine frame, excepting
that they have no attachment to prevent them
from being worn by the motion of the boxes up and
down in the jaws. Fig. 186 is a horizontal section,
fig. 187 a plan, and fig. 188 a transverse section[77] of a
truck. The frame C D E F, fig. 187, shown also at
h′ h′, figs. 186 and 188, is of rectangular form and is
forged in one piece. The legs f f which form the
jaws for the boxes, are bolted to the frame as shown
in fig. 186. To the lower end of these legs a brace,
g g g, is bolted, which thus unites them together.
On each side one spring, S F S, is placed under the
frame and in the reverse or inverted position to that
of the driving-springs. A pair of equalizing levers,
G G G, is placed on each side of the truck, one of them
on the inside of the frame and the other on the outside,
as shown in the plan. The ends of these equalizers
rest on the top of the truck-boxes, and the
springs are attached to the levers at i i by the hangers,
j j. The truck-frame rests on the top of the spring-strap,
F, which is made of the form of an arc of a circle,
or “rounded,” as it is termed by workmen, so that
it can move freely about the point of support. It is
evident that this arrangement of spring and equalizer
operates in the same way as that employed for the
driving-wheels in distributing the weight on each of
the wheels, and that the truck-frame is supported on
two points, k, k, figs. 186 and 187. The weight of the
front end of the engine rests on a cast iron centre-plate,
H H. This centre-plate rests on four bars, l l,
l l, and m m, m m, two of which are bolted to the frame
transversely and the other two longitudinally, as shown
in the plan. These bars are elevated in the centre as
shown in figs. 186 and 188. The transverse bars are
trussed with two corresponding bars, n n, fig. 188, below.
These truss-bars as they are called, are bolted to
the upper bars with bolts, o, o, but are separated from
the top-bars by distance pieces, P, P, figs. 186 and 188.
The centre-plate H H, called the lower centre-plate,
has an annular groove in it, which receives a corresponding
projection on the casting K K, called the upper
centre-plate, which is bolted to the bed-plate of the
cylinders, as shown in plate II. The upper centre-plate
has a pin, y, called a centre-pin, fig. 186 and
plate II, attached to it, which passes through the lower
centre-plate, and has a key underneath the latter
plate. This key is intended to prevent the engine
from “jumping” off of the truck on a rough track or in
case of accident. The annular groove and the projection
which fits into it are intended to receive the
strain which otherwise would bear against the centre-pin
and would be liable to break or bend it.
[76] In some rare cases three pairs of wheels are employed for locomotive
trucks. Six-wheeled trucks are very commonly used under passenger
cars.
[77] The right half is a section through the centre of the axle, or of G g,
of fig. 186, and the left half a section through the centre of the truck, or
on g g, of fig. 186.
From this description it will be seen that while the
truck-frame rests on two points, k and k, the weight of
the engine is supported by the centre-plate of the
truck. As the back part substantially rests on the
centres of the two equalizers, it will be seen that this
distribution of the weight fulfills the conditions of the
tripod, or as it has been called, the “three-legged principle.”
Fig. 189.
Fig. 190.
Fig. 191.
Scale ³⁄₈ in. = 1 foot.
Question 306.How are trucks arranged so as to give
them lateral motion?
Answer. When this is done, the lower centre-plate
is usually suspended in some way from the truck-frame
on links or hangers, so that it can swing laterally.
One method of doing this is shown in figs. 189, 190
and 191. Fig. 190 is a front view,
fig. 191 a plan,
and fig. 189 a transverse section of such an arrangement.
The centre-plate H H has cast with it an
extension, B B, the ends of which are suspended on
links, L, L, called suspension-links, the upper ends of
which are attached to bars, m, m, which are set edgeways
and extend across the truck-frames. It is evident
that with this arrangement the lower centre
casting can swing crosswise of the track on the links
L, L, and that the front end of the engine will thus
have a lateral motion independent of the truck.
PART XIII. ADHESION AND TRACTION.
Question 307.What is meant by the “adhesion” of
a locomotive?
Answer. It is the resistance which prevents or opposes
the slipping of the driving-wheels on the rails,
and is due to the friction of the former on the latter.
Question 308.On what does the amount of this friction
depend?
Answer. Like all friction it depends upon the
weight or pressure of the surfaces in contact, and consequently
upon the load which rests on each wheel.
It also depends upon the condition of the rails, and
probably to some extent upon the material of which
they and the tires on the wheels are made.
Fig. 192.
Scale ¹⁄₄ in. = 1 foot.
Question 309.How much force is required to make
the driving-wheels of a locomotive slip on an ordinary
railroad track?
Answer. The force required to make them slip will,
as already stated, vary very much with the condition
of the rails. If they are quite dry and clean it will
require a force equal to about one-fourth the weight
on the wheels. That is, supposing we have a wheel,
A B, fig. 192, attached to a frame which is fastened so
that it cannot move, and that the wheel rests on a rail
and is loaded with say 10,000 pounds, if now a rope or
chain could be attached at a point, B, exactly at the
tread of the wheel, and carried over a pulley, C, then
it would require a weight, D, of about 2,500 pounds
attached to the end of the rope to make the wheel
slip. If the rails were sanded, the adhesion would be
somewhat greater, and if they were wet or muddy or
greasy, considerably less. For ordinary circumstances
the adhesion may safely be assumed to be one-fifth of
the weight of the driving-wheels. Of course the total
weight on all the driving-wheels must be taken in calculating
the adhesion. Thus, if a locomotive has four
driving-wheels and each one of them bears a load of
10,000 pounds, then the total weight on the driving-wheels,
or adhesive weight, as it is called, will be
10,000 × 4 = 40,000 pounds, and the adhesion will be
40,0005 = 8,000 pounds.
Question 310.What is meant by the tractive power
of a locomotive?
Answer. It is the force with which the locomotive
is urged in a horizontal direction by the pressure of
the steam in the cylinders, and which therefore tends
to move the locomotive and draw the load attached to
it.
The tractive power is of course due to the pressure
of steam on the piston, and therefore its amount is
dependent upon the average steam pressure in the cylinder,
on the area of the piston, and also on the distance
through which the pressure is exerted, or, in
other words, on the stroke of the piston. Thus if we
have a cylinder 16 inches in diameter and two feet
stroke and an average steam pressure of 50 pounds
per square inch, then as the area of such a piston
would be 201 square inches, the average pressure on
it would be 201 × 50 = 10,050 pounds, and as each piston
moves through four feet during one revolution of
the wheels, the number of foot-pounds of energy exerted
by it would be 10,050 × 4 = 40,200, and for the
two cylinders of a locomotive double that amount, or
80,400 foot-pounds. Now if the driving-wheels are
five feet in diameter, their circumference will be
15.7 feet, and therefore the locomotive will move
that distance on the rails during one revolution, if the
wheels do not slip. The 80,400 foot-pounds of energy
is therefore exerted through a distance of 15.7 feet,
and therefore
80,40015.7 = 5,121 pounds,
which is the force exerted through each foot that the
circumference of the wheel revolves and the locomotive
moves. If the wheels were only half the diameter,
or 2¹⁄₂ feet, then their circumference would be
7.85 feet and the tractive power would be
80,4007.85 = 10,242 pounds,
or double what it was before. It will be seen, then,
that the tractive force of a locomotive is dependent
upon (1) the average steam pressure in the cylinders,
(2) the area, (3) the stroke of the pistons, and (4) the
diameter of the driving-wheels.
Question 311.How is the tractive power of a locomotive
calculated?
Answer.By multiplying together the area of
the piston in square inches, the average steam
pressure in pounds per square inch on the piston
during the whole stroke, and four times
the length of the stroke of the piston,[78] and
dividing the product by the circumference of
the wheel. The result will be the tractive power
exerted in pounds. The adhesion must of course always
exceed the tractive force, otherwise the wheels
will slip.
[78] This length may be taken in feet, inches or any other measure, but
in making the calculation the circumference of the wheel must be taken
in the same measure as the stroke of the piston.
Question 312.How is the locomotive made to advance
by causing the wheels to revolve?
Answer. The pressure of steam in the cylinders is
exerted in one direction against the piston, and in the
opposite direction against the cylinder head, as shown
in fig. 192, in which the steam is represented by the
dotted shading in the back end of the cylinder, and
the direction of the pressure by the darts s, s. The
pressure against the piston is communicated by the
connecting-rod to the crank-pin E, and that on the
cylinder-head is carried to the axle by the frame F F′,
and the direction of the two forces is indicated by the
two darts, a and b. We may now regard the spokes
of the wheels as acting as levers, and assume that the
fulcrum is either at the centre G of the axle, or at B,
the point of contact of the wheel with the rail.[79] We
will assume that it is at the centre G of the axle and
for the sake of even figures that the wheel is six feet
in diameter and cylinders have two feet stroke. We
will also suppose that the engine is supported so that
the wheels do not touch the rails, and that a chain or
rope passing over a pulley C is attached to the wheels
at B and with a weight at D. We now have a force,
a, of 10,000 pounds exerted on the crank-pin, or at
the end of the short arm E G of the lever E G B.
As E G is one foot and G B three feet long, 10,000
would be balanced by
10,000 × 13 = 3,333 pounds,
at B. In other words, it would require 3,333 pounds
suspended from the chain at D to resist the strain at
E. But when this is the case, the pressure of the axle
at the fulcrum, in the direction of the dart c, is equal to
the pressure against the crank-pin E added to that
exerted by the weight D at B, or 10,000 + 3,333 =
13,333 pounds.
[79] The question whether the centre of the axle or the point of contact
with the rail is the fulcrum of the lever in this case has been the subject
of much animated discussion and contention. As the word fulcrum
means “a point about which a lever moves,” it is believed that the dispute
is due simply to a difference in the meaning assigned to the word
fulcrum. If we regard the fulcrum as the point which is fixed in relation
to the locomotive, then it is at the centre of the axle, but if we refer
it to the surface of the earth, then it is at the top of the rail.
As the pressure against the axle in the opposite direction,
b, is only 10,000 pounds, there will be an unbalanced
force of 3,333 pounds acting in the direction
of the dart c, and tending to move it that way. As
the axle is attached to the locomotive frame, this force
will of course have a tendency to move the whole machine,
and is really the tractive force of the engine.
If, on the other hand, we regard the point of contact
B of the wheel with the rail as a fulcrum, we have a
force of 10,000 pounds acting against a lever, E G B,
four feet long. There would therefore be a force, c, of
10,000 × 43 = 13,333 pounds
exerted at G, and as the pressure in the direction of
the dart b is only 10,000, there would be an unbalanced
strain of 13,333 - 10,000 = 3,333 pounds acting
against the axle in the direction of the dart c, or, in
other words, there is 3,333 pounds more of force pulling
the axle forward than there is pushing it backward.
When the crank-pin is below the axle, in the position
shown in fig. 193, then if the centre of the axle
is regarded as the fulcrum we have a pressure of
10,000 pounds pushing against the front cylinder-head,
which is transferred to the axle by the frames,
and acts in the direction of the dart c, and we also
have a pressure against the crank-pin E in the direction
of the dart a. Now 10,000 pounds at E would
exert a force of
10,000 × 13 = 3,333 pounds
at B and
10,000 × 23 = 6,666 pounds
at G in the direction of b. But the pressure on the
cylinder-head pulls against the axle G in the direction
c with a force of 10,000, so that the excess of
strain in the direction b will be equal to 10,000 -
6,666 = 3,333 pounds. If we regard B as the fulcrum,
the calculation is exactly the same, as 10,000 pounds
at E exerts a force at G equal to
10,000 × 23 = 6,666 pounds,
and the difference between it and the pressure exerted
by the strain against the front cylinder-head is the
force which urges the axle and with it the locomotive
forward.
It will be seen, then, that it is immaterial which point
is regarded as the fulcrum, as the result of the calculations
is exactly the same.
Fig. 193.
Scale ¹⁄₄ in. = 1 foot.
It must not, however, be hastily supposed from
what has been said that the total pressure against
the axle can be greater than its resistance to the pressure.
As soon as the one exceeds the other it will
move. But supposing that it requires a force equal to
3,333 pounds to draw a train coupled to the engine,
as soon as the difference between the force exerted
against the axle by the piston to move it forward and
that which presses it back exceeds 3,333 pounds, the
locomotive will move the train. If it continues to
exceed it the speed of the train will be accelerated and
thus the resistance which holds the engine back and
that which pushes it forward will always be equal.
Question 313.Does the fact that the piston is working
from the end of a longer lever E G B, fig. 192, when
the crank-pin is above the axle, enable the locomotive to start
a heavier train than when the crank-pin is below the axle
and the piston is working against a shorter lever, G E B,
fig. 193?
Answer. No; because, as has already been shown,
the pressure against the axle is the same in both cases.
It is in fact only during the forward stroke that the
pressure on the crank-pin moves the engine forward.
The forward pressure which is exerted by the crank-pin
at the axle is then greater than that exerted
against the latter in the opposite direction by the cylinder-head
and frames. It is this excess of crank
pressure which moves the engine and which is the
tractive force during the forward stroke. During the
backward stroke the piston is pushing the axle backward,
and the pressure against the front cylinder-head
is pulling it forward. The latter then exceeds the
former, and the difference between the two is the force
which moves the engine forward. As has been shown,
this difference is the same in both positions of the
crank, and therefore the locomotive can not from this
cause pull more when the crank is above the axle than
when it is below.
PART XIV. INTERNAL DISTURBING FORCES IN THE LOCOMOTIVE.
Question 314.What are the internal disturbing forces
in a locomotive?
Answer. They are: 1, the momentum of the parts
which have a reciprocating motion; 2, those due to
the varying pressure of the steam in the cylinder-heads;
3, those caused by the thrust of the connecting-rods
against the guide-bars; and 4, those produced
by unbalanced revolving parts.
Question 315.How can the effects of these disturbing
forces be neutralized?
Answer. By putting counterweights, A, A, fig. 161,
in the driving-wheels opposite the crank-pins. The
motion of these will then be in the reverse direction
to that of the weight of the parts attached to the
crank-pins, and the motion of the one will thus, to
some extent, at least, neutralize the disturbing influence
of the other.
Question 316.Can the weight of these counterweights
be calculated for any locomotive?
Answer. It can probably be calculated, but it is an
exceedingly complicated problem, and one about which
there is much difference of opinion. The difficulty is
also increased by the fact that while counterweights
may be heavy enough for one speed, they may be too
heavy or too light for a slower or faster speed, and
quite disproportioned when the engine is not working
steam. The following rules are given in “Clark’s
Railway Machinery,” and are perhaps sufficiently close
to find a first approximation to the requisite position
and weight of the counterweights; but the final adjustment
should be made by trial. This can be done
by suspending the locomotive by chains attached to
the four corners of its frame, and setting the machinery
in motion at the speed it is intended to run.
By attaching a pencil to one or to each of the four
corners of the frame, and arranging it so that it will
mark on a horizontal fixed card, a diagram will be
drawn, being usually an oval, which will show the
amount and form of the oscillations. The counterweights
can then be adjusted so that the diagram drawn
by the pencil is reduced to the least possible size.
When the adjustment is successful, the diameter of
the diagram is reduced to about ¹⁄₁₆ of an inch.[80] Another
and simpler, but less accurate, way is to place a
pail or other vessel filled with water on the front
of the engine and run the locomotive on a smooth
track at a high speed, and adjust the counterweights
so that the least amount of water will be
spilled.
Question 317.How can the centre of gravity of a
counterweight in one segment be found?
Answer.By cutting a wooden templet of uniform
thickness to the form of the surface,
and freely suspending it by one of the corners,
a, as in fig. 194; a plummet-line, P a,
dropped from the same point of suspension
in front of the templet will intersect the
centre lineb cat the centre of gravityC.
Fig. 194.
Question 318.How can the centre of gravity of a
counterweight in three segments be found?
Answer.Find the centre of gravityC, fig.
195, of one of the counterweights, as above;
throughCstrike an arc from the centre, a,
of the wheel, crossing the centre lines of
the other segments at their centres, C′ C″;
drawC′ C″meetingA BatD, and set offD E, one-third of the intervalD C. ThenEis the common centre of gravity of the three
segments.
Fig. 195.
Question 319.How can the centre of gravity of a
counterweight in two segments be found?
Answer. This is required when the crank is opposite
to a spoke, as in fig. 196. Find the centre of
gravity, C, of one segment as before, and by
an arc find the other centreC′; drawC C′,
cuttingA BatD, which is the common centre
of gravity.
Fig. 196.
Question 320.How can the centre of gravity of a
counterweight in four segments be found?
Answer.Find, as before, the centresC, C′, C″,
C‴, fig. 197, of the segments; drawC″ C′andC‴ C, cutting the lineA B; bisect the interval
so inclosed atEfor the common centre
of gravity.
Fig. 197.
Question 321.How is the counterweight for outside-cylinder
engines with a single pair of driving-wheels calculated?
Answer.Find the total weight, in pounds, of
the revolving and reciprocating masses for
one side, namely, the piston and appendages,
connecting-rod, crank-pin and crank-pin boss;
multiply by the length of crank in inches, and
divide by the distance in inches of the centre
of gravity of the space to be occupied by the
counterweight. The result is the counterweight
in pounds, to be placed exactly opposite
to the crank.
Question 322. How is the counterweight for outside-cylinder
engines with coupled driving-wheels calculated?
Answer. Find the separate revolving weights,
in pounds, of crank-pin, crank-pin boss, coupling-rods
and connecting-rod, for each wheel,
also the reciprocating weight of the piston
and appendages, and half the connecting-rod;
divide the reciprocating weight equally between
the coupled wheels, and add the part,
so allotted, to the revolving weight on each
wheel; the sums so obtained are the weights to
be balanced at the several wheels, for which
the necessary counterweight may be found by
the preceding rule.
Question 323. How are the counterweights constructed?
Answer. They are usually made of cast iron, so as to
fill or partly fill the spaces between the spokes of the
wheel, as shown at A A in fig. 161. Each of the segments
consists of two pieces, one of which is put in
from the outside of the wheel and the other from the
inside. The two are then bolted together with bolts,
which are shown in the above figure. In some cases
the counterweights are cast solid with the wheels, and
in others, cavities are cast in the wheels which are
filled with lead, which is poured in when melted.
Some locomotive builders make the rims and spokes
of the wheels hollow and fill them with lead opposite
to the crank-pins. It is difficult, however, to get the
required weight in such wheels unless they are of
large diameter.
Question 324.What effect has the strain on the draw-bar,
when the engine is pulling a load, upon the distribution
of the weight on the wheels?
Answer. It has the effect of pulling the back end of
the engine down, and, as it is balanced on the fulcrums
of the equalizing levers, it at the same time lifts up
the front end. In this way the harder a locomotive
is pulling the greater will be the weight which is
thrown on the driving-wheels, and that on the truck
will be correspondingly diminished. The higher the
draw-bar is above the rails the greater will be the tendency
to pull the engine down behind and up in front.
PART XV. MISCELLANEOUS.
Question 325.What is the sand-box, V, plates I and
II for, and how is it constructed?
Answer. It is intended to carry a supply of dry sand,
which is scattered on the rails in front of the driving-wheels
when the latter are liable to slip. This is done
by two pipes, e′, e′, plate I, one on each side of the engine.
They lead from the sand-box to within a few
inches of the rail. At the upper end and inside the
sand-box they each have a valve which is operated by
a lever which is connected to the cab by a rod which
enables the locomotive runner to open or close the
valve at pleasure.
The sand-box is usually made of sheet iron with a
cast iron base, and a top of a more or less ornamental
design. It also has an opening on top through which
the sand is supplied to the box. This opening has a
loose cover to exclude rain and dirt from the sand.
The sand-box is usually located on top of the boiler in
front of the front driving-wheels.
Answer. It is used for giving signals of the starting
or approach of the engine. It also is located on top
of the boiler and is usually hung on a cast iron
frame and rung with a rope connecting it with the
cab.
Question 327.What is the weight of an ordinary
locomotive bell?
Answer. From 50 to 100 pounds.
Question 328.What is a locomotive head-light?
Answer. It is a large lamp, T, plates I and II,
placed in front of the locomotive to signal its approach
at night and also to illuminate the track for the locomotive
runner.
Fig. 198.
Scale 1¹⁄₂ in. = 1 foot.
Question 329.How is a head-light constructed?
Answer. The lamp has what is called an Argand
burner; that is, a burner with a hollow cylindrical
wick, through the centre of which a current of air circulates,
which thus supplies the flame with a larger
quantity of air than is possible if the latter can come
in contact with the former only from the outside. The
result is that the combustion is much more brilliant
than with ordinary burners. In order to throw all the
light on the track the burner is placed inside of a concave
reflector, a b c, fig. 198, which is of a parabolic
form. One of the peculiarities of this form of reflector
is that if a light is placed in its focus f the rays will
be reflected from its surface in parallel lines. Thus, let
a b c, fig. 198, represent a section of such a reflector.
Now, if a light be placed in the focus f the rays will
strike against the reflector, be thrown in the direction
of the dotted lines f 1 x, f 2 x ... f 9 x, etc., and thus
be thrown directly in front of the engine. The reflectors
are usually made of copper and plated with silver.
The lamps and reflectors for head-lights are inclosed
in a rectangular case which is supported on two brackets
bolted to the front of the smoke-box. On these
brackets a wooden shelf is fastened on which the head-light
rests.
Question 330.What are the running-boards and hand-rails?
Answer. The running-boards are planks, i i, plate I,
placed on each side of the boiler to enable the locomotive
runner or fireman to go from the cab to the front
end of the engine when it is running. The hand-rails,
m m′ m′, are brass or iron pipes attached to the top of
the boiler and extending from the cab to the smoke-box,
and are placed there, as their name indicates, to support
or for a hand-hold for persons on the running-board.
Question 331.What provision is made for removing
from the track such obstacles as cattle or fallen rocks,
which may be in front of locomotives?
Answer. What is called a cow-catcher or pilot, S,
plates I and II, is attached to the front of the locomotive.
This is usually made of wood, and consists
of a triangular frame at the bottom which is supported
about four inches above the tops of the rails.
Straight pieces of wood of about 2¹⁄₂ × 4 inches section
are fastened to this frame and also to a horizontal
piece which is bolted to the bumper-timber E′. These
pieces arranged in this way and only a few inches
apart give to the cow-catcher a peculiar curved
form somewhat resembling that of the mould-board of
a plow, which is very well adapted for throwing any
obstacles from the track. Sometimes these pieces are
placed horizontally instead of being inclined up and
down. Cow-catchers are also in some cases made of
round iron bars or angle iron. They are always
bolted securely to the bumper-timber and strengthened
by strong iron braces attached to the bottom frame at
the front and back. These braces are usually fastened
at the other end to the bumper-timber, but are sometimes
attached to the bed-plates of the cylinder.
There is also usually a strong pushing-bar attached
with a bolt and hinged joint to the bumper-timber.
This is shown in plates II and III in the position it
occupies when not in use. It is used in pushing cars,
as very often there is not room for the pilot under the
end of the car. In using it is raised up, and the front
end is then coupled to the draw-head of the car.
Fig. 199.
Question 332.What is the foot-board or foot-plate of
a locomotive?
Answer. It is a wrought or cast iron plate which extends
across and rests upon the two frames at the
back part of the locomotive and behind the boiler,
and on which the locomotive runner and fireman
stand. It also unites the two frames very securely,
and furnishes an attachment for the draw-bar. The
foot-board is often made much heavier than is necessary
for strength, in order to increase the weight,
and thus the adhesion, on the driving-wheels. It is
a fact often not suspected that any weight placed on
the back end of an ordinary locomotive will increase
the load on the driving-wheels by an amount considerably
greater than that of the weight itself. The
reason of this is that the locomotive rests on the
centre of the truck and the centres of the equalizers,
and therefore the weight, if applied to the back end of
the engine, gains considerable leverage. This will be
clear if we take a beam, A B, and rest it on two supports,
m and n, fig. 199. If now we put a weight W
on the end, overhanging the point of support, the
weight which will rest on n will be equal to that of W
multiplied by its distance C from m and divided by
the distance D between m and n. Thus if a foot-board
weighs 1,000 pounds, and its centre of gravity is 5¹⁄₂
feet behind the centre of the equalizer, and the latter
14 feet from the centre of the truck, then the
weight thrown on the driving-wheels will be equal to
1,000 × 19¹⁄₂14 = 1,393 pounds.
The same thing is of course true of any other weight
placed on the back end of the engine.
Question 333.What are the “wheel-guards” of a
locomotive?
Answer. They are sheet iron covers over the upper
half of the periphery or tread of the wheels, and are
placed there to protect the engine from the dirt and
mud which adhere to the wheels and are then thrown
off on the machinery by the centrifugal force.
Question 334.What are “check” or “safety chains?”
Answer. There are two kinds of such chains, the
one attached to the trucks and frames of the locomotive
and the tender. The object of these chains is to
prevent the trucks from turning around and getting
crosswise of the track if the trucks should leave the
rails. The other kind of safety chains connects the
engine to the tender, so that, in case the draw-bar or
coupling-pins should break, the two will not separate.
Great care should be exercised to attach the truck
chains so as to be strong enough to resist the strains
to which they will be subjected in case the trucks run
off the track. The grossest carelessness and ignorance
are often shown in the construction of these
parts.
PART XVI. SCREW-THREADS, BOLTS AND NUTS.
Question 335.How must the screws of bolts and nuts
be made, in order to fit each other?
Answer. Each size of screw must be made of exactly
the same diameter, and their threads of the same form
and proportions and pitch.
Question 336.What is meant by the “pitch” of a
thread?
Answer. It is the distance the thread progresses
lengthwise of the screw in one revolution. Thus if a
single-threaded screw has one-eighth of an inch pitch,
it means that the threads are ¹⁄₈ of an inch apart
measured from the centre of one thread to the centre
of that next to it, and therefore there are eight
threads to each inch in length of the screw.
Question 337.What is meant by a “single-threaded”
screw?
Answer. It means a screw with but one thread instead
of two or more. Thus if we take a string and
wind it around a pencil, it will represent a single-threaded
screw, and if we take two or three strings
and wind them parallel to each other, they will represent
a double or treble-threaded screw. The latter
kinds are seldom or never used on locomotives, so
that in the following discussion only single-threaded
screws will be referred to.
Fig. 200.
Full Size.
Question 338.What is the usual form of the threads
of screws?
Answer. The most common is what is called the
V-thread, represented in fig. 200, which is made
sharp at both the top and bottom. If such a thread
for one screw is made very pointed and that for
another is blunt, it is plain that the nut for the
one will not fit the other accurately, and also that if a
nut has eight threads to the inch, it will not fit on
a bolt with nine. Owing to the fact that, until within
a few years, no common standard has been agreed
upon for the form, proportions or pitch of screws
there has been very great diversity in these respects
in the screws which have been used in the
construction of locomotives and other machinery.
In 1864 the inconvenience and confusion from this
cause became so great that it attracted the attention
of the Franklin Institute of Philadelphia, and a committee
was appointed by that association to investigate
and report on the subject. That committee
recommended the adoption of the Sellers system of
screw-threads and bolts, which was devised by Mr.
William Sellers, of Philadelphia. This same system
was subsequently adopted as the standard by both the
Army and Navy Departments of the United States,
and then by the Master Mechanics’ and Master Car
Builders’ associations, so that it may now be regarded,
and in fact is called, the United States standard, but
the design is due to Mr. Sellers.
Question 339.In establishing a standard system of
screws and threads, what is the first thing which must be
determined?
Answer. The number of threads to the inch, or the
pitch of the threads for screws of different diameters.
Fig. 201. Full size.
Question 340.What is the standard for the number
of threads to the inch for the different sized screws of the
Sellers system?
Answer. The number of threads with their other
proportion is given in the table at the end of this
chapter on page 348.
Question 341.What is the form of the thread of this
standard?
Answer. The form is shown in fig. 201, and is similar
to the V-thread, excepting that it is flattened at
the top and bottom.
Question 342.What are the reasons for the adoption
of this form of thread?
Answer. It has already been pointed out that if a
screw is made with a “blunt” thread it will not fit a
nut with very acute or “sharp” threads; or, if the
thread of the bolt was acute and that in the nut obtuse,
they would fit imperfectly. It is therefore
necessary in a standard system to fix upon the angle
which the sides of the thread shall bear to each other.
This in the United States standard system was determined
by Mr. Sellers at 60 degrees, because that angle
is easily laid off without special instruments[81] and is
perhaps as good as or better than any other form for
the threads.
[81] This can be done by drawing a circle of any diameter, and subdividing
the circumference into six equal parts with the radius. Lines,
drawn from the points of division to the centre will have an inclination
of 60 degrees to each other.
It is obvious that if a tool is ground with its sides
at an angle of 60 degrees to each other, if the point is
made sharp after a very little use it will be worn more
or less so that the bottom of the thread will not be
cut perfectly sharp, and therefore it will be difficult to
make bolts and nuts with sharp threads fit each other
accurately. It is also plain that the sharp edge of a
thread gives very little strength to the screw, and yet
diminishes that of the bolt very materially. It will
also be impossible to measure the diameter of the
screw at the bottom of the thread if it is made sharp,
as its depth will vary as the point of the tool wears,
and it is almost impossible to measure the diameter of
such a screw accurately with ordinary calipers. A
sharp-edged thread in a bolt is also very liable to be
injured and bruised by coming in contact with other
objects. To obviate these evils the standard threads
are therefore made flat on the top, and it is evident
that a similar shape at the bottom will give increased
strength to the bolt as well as conform to and fit the
thread in the nut. To give this form requires only
that the point of the cutting tool shall be taken off,
and then it is evident this form of thread can be cut
in a lathe with the same tool and in the same manner
as the sharp thread. The width of the flat top and
bottom should of course bear a definite proportion to
the size or pitch of the thread.
Fig. 202.
Question 343.What are the proportions of the
standard threads?
Answer. The rule given by Mr. Sellers for proportioning
the thread is as follows: “Divide the pitch,
or, what is the same thing, the side of the
thread, into eight equal parts; take off one
part from the top and fill in one part in
the bottom of the thread: then the flat top
and bottom will equal one-eighth of the
pitch, the wearing surface will be three-quarters
of the pitch and the diameter of
screw at bottom of the thread will be expressed
by the formula:
diameter - 1.299no. threads per inch.”
In order to make the form and proportions of this
standard thread as plain as possible, we have had an
enlarged diagram, fig. 202, engraved, so as to represent
the different parts clearly. x represents the pitch, d
the diameter of the screw in inches, v the number of
threads to the inch, n the diameter at bottom of
thread, m the width of back part of thread at the top
and bottom, and s the length of the side of thread.
From Mr. Sellers’ rule the following formulæ can be
deduced:
n = d - 1.299v
m = x8
s = 3x4
From this rule any thread can be constructed, it
being only necessary to know the pitch or number of
threads to the inch. This, with all the dimensions of
the standard threads for bolts from ¹⁄₄ to 2 inch diameter,
is given in the table on page 348.
For practical use in the shop a gauge like that shown
in fig. 203 will be found most convenient for grinding
the tools to the proper form for making the standard
screws. With this gauge the screw-cutting tool can
first be ground to the proper angle by fitting it to the
deepest notch, and the requisite quantity should then
be taken off the point by fitting it to the notch representing
the form of thread for the sized bolt or number
of threads to the inch which it is intended to cut.
Wherever this standard for threads is used, if any pretense
at all is made to accuracy of workmanship, careful
attention should be given to the form and proportion
of the threads as well as to the number to the
inch. In buying taps and dies the purchaser should
see that they conform in every respect to the standard,
and in making specifications for new work similar
care should be exercised to secure the true standard,
form and proportion of screws. In many shops the
workmen who have the care of those tools are entirely
ignorant of the peculiarities of the Sellers system, and
have only the vague idea that so long as they get the
proper number of threads to the inch they are doing
all that is necessary to secure uniformity. Unless,
therefore, some care is exercised to insure accuracy of
workmanship in this department, the adoption of a
“standard” for screws will not insure the advantages
which would result from uniformity of screws and
threads.
Fig. 203. Full size.
Question 344.How thick must a nut be, measuring
lengthwise of the bolt, so that the thread in the nut will be
of equal strength to that of the bolt?
Answer. Its thickness must be equal to the outside
diameter of the screw.
TABLE GIVING PROPORTIONS OF THE UNITED STATES OR SELLERS
STANDARD SYSTEM OF SCREW-THREADS.
Outside diameter of screw in inches
Number of threads per inch
Diameter of screw at the root of the thread in decimals of an inch
Width of top and bottom of thread in decimals of an inch
¹⁄₄
20
.185
.0062
⁵⁄₁₆
18
.240
.0074
³⁄₈
16
.294
.0078
⁷⁄₁₆
14
.344
.0089
¹⁄₂
13
.400
.0096
⁹⁄₁₆
12
.454
.0104
⁵⁄₈
11
.507
.0113
³⁄₄
10
.620
.0125
⁷⁄₈
9
.731
.0138
1
8
.837
.0156
1
¹⁄₈
7
.940
.0178
1
¹⁄₄
7
1
.065
.0178
1
³⁄₈
6
1
.160
.0208
1
¹⁄₂
6
1
.284
.0208
1
⁵⁄₈
5
¹⁄₂
1
.389
.0227
1
³⁄₄
5
1
.491
.0250
1
⁷⁄₈
5
1
.616
.0250
2
4
¹⁄₂
1
.712
.0277
PART XVII. TENDERS.
Question 345.What are locomotive tenders for?
Answer. They carry a supply of fuel and water for
locomotives while they are running.
Question 346.How are they usually constructed?
Answer. Their construction is represented in figs.
204, 205 and 206. Fig. 204 is a side view, fig. 205 a
longitudinal section, and fig. 206 a plan of an ordinary
tender, which consists of a frame, A A A A, made of
wood or iron,[82] mounted on a pair of trucks, T, T.
The top of the frame is covered with planks, B, B,
which form the floor of the tender. On top of this
floor a sheet-iron tank, C C C, is placed, which carries
the supply of water. This tank is made somewhat
in the form of a letter ⊃, as shown in the plan.
It is made in this way so that the space between the
two branches, C, C, or “legs,” as they are called, will
give room for fuel. Around the upper edge of the
tank a sheet-iron rim, D D, is riveted, so as to prevent
the fuel from falling off when it is filled up above
the top of the tank.
[82] The frame represented in the engraving is made of wood. In the
plan it is shown by dotted lines.
Question 347.How is the tank filled with water?
Answer. There is a round opening, E, called a man-hole,
on top. Into this the end of a leather or canvas
hose is introduced, which is attached to a stationary
tank, at a water station, and a stream of water is then
allowed to flow through the hose into the tank of the
tender.
Question 348.How is the water conducted from the
tender to the engine?
Answer. To each side of the front end of the tank,
one end of a piece of rubber hose, F F, is attached,
which is connected at the other end to the pipe on the
engine which supplies the pump with water. The
opening inside the tank through which the water
flows to the hose is covered with a valve, which is not
shown in the engraving, but which is operated by a
lever or handle, G. The valve is covered with a hood
or strainer, perforated with small holes, which is intended
to prevent dirt from entering the hose and thus
getting into and obstructing the pump. The hose is
connected to the supply pipe by a screw-coupling similar
to that used with ordinary fire-engine hose.
Question 349.How are the flat sides of the tank
strengthened so as to resist the pressure and weight of the
water?
Answer. They are sometimes braced or stayed with
rods or bars, a, a, and h, h, fig. 205, extending from
one side to the other and from the top to the bottom,
and angle or ⊤ iron is also riveted to the sides to stiffen
them.
Question 350.How is the tender connected to the engine?
Answer. By the draw-bar, H, and coupling-pin, o,
fig. 205, and also by the safety chains, d.
Fig. 204. Scale ¹⁄₄ inch = 1 foot.
Fig. 205. Scale ¹⁄₄ inch = 1 foot.
Fig. 206. Scale ¹⁄₄ inch = 1 foot.
Question 351.In what respect do the tender trucks
differ from the engine truck?
Answer. Chiefly in having the journal-bearings and
frames outside of the wheels.
Fig. 207. Scale ³⁄₁₆ in. = 1 inch.
Fig. 208. Scale ³⁄₁₆ in. = 1 inch.
Question 352.Why are the bearings placed outside
instead of inside?
Answer. Because they are then more accessible than
if they are inside, and the oil-boxes on the axles can
be entirely closed over the ends of the axles, so that
no oil can leak out, whereas if the boxes are inside,
they must be left open at both ends. When the boxes
are on the outside, they can be oiled, or a journal-bearing
can be removed and a new one put in its
place, with much less difficulty than if the boxes were
on the inside of the wheels. The only reason why the
bearings of engine truck-axles are placed inside the
wheels is because they would be in the way of the
cylinders if they were outside.
Question 353.How are the axle-boxes for the tender
axle constructed?
Fig. 209. Scale ³⁄₁₆ in. = 1 inch.
Answer. Their construction is similar to that of a
car axle-box, the standard form of which is represented
in figs. 207, 208 and
209. Fig. 207 is a section
lengthwise of the axle, fig. 208 a section crosswise
of the axle, and fig. 209 a sectional plan. A is the
journal of the axle, which is inclosed by a cast iron
box, K K, which is open in front and at the back.
The front has a cover, H, which is either fastened by a
spring, as shown in the illustrations, or is bolted to
the box. The axle enters the box from the back, I,
and has either a wood or leather packing, J J, called
a dust-guard, to keep the dust from getting in and the
oil from leaking out of the box. D is a brass journal-bearing,
which rests against a cast iron bearing piece
or key, E, which is put in so that by removing it
through the opening F F, the brass bearing can be
raised up high enough to clear the collar, G, on the
end of the axle and thus be removed in the same way.
The lower portion, L, of the box under the axle is
usually filled with cotton or woolen waste saturated
with oil. This constantly presses against the axle,
and thus keeps it oiled.
Question 354.How are the tender trucks constructed?
Answer. They are made of various patterns, some of
which have wooden frames and in other cases the
frames are made of iron. The truck illustrated in our
engraving, figs. 204 and 205, is made of iron and is
very similar to the engine truck, excepting, as already
stated, the frames are outside instead of inside of the
wheels.
Question 355.How is the tender supported on the
trucks?
Answer. It rests on the centre of the front truck and
on a bearing, n, fig. 204, on the frames on each side of
the back truck. This arrangement gives three bearing
points, the advantages of which have already been
explained. A truck which supports the load which it
carries in the centre is said to be centre-bearing, and if
the load is carried on each side, side-bearing.
Question 356.How are the brakes attached to the
tender?
Answer. They are attached usually to the back truck
alone, but in some cases to both trucks, and are operated
by a wheel, N, fig. 204, and a shaft which extends
below the tender frame and on which a chain
attached to the brakes is wound.
Question 357.How much water and coal does an
ordinary tender carry?
Answer. A tender for a thirty-ton engine carries
from 1,500 to 2,000 gallons of water and three to four
tons of coal, and weighs from 40,000 to 45,000 pounds
loaded. An engine of this kind and its tender therefore
weigh about 100,000 pounds, which, being even
figures, can easily be remembered.
PART XVIII. FRICTION AND LUBRICATION.
Question 358.What is meant by friction?
Answer. Friction is the resistance between two
bodies in contact which opposes the sliding of the
one on the other. Thus if a brick is placed on a board
with a slight inclination, it will not slide because the
friction between them, or the resistance opposed to
motion, is greater than the force exerted by the
weight of the brick to move it downward. If, however,
the inclination of the board is increased sufficiently
so that a larger proportion of the weight of
the brick urges it downward, then the friction will be
overcome, and it will slide. When the brake-blocks
of a car are pressed against the wheels, they produce
friction, which resists the revolving motion of the
wheels and will ultimately stop the car; and when the
weight of an engine is supported on the driving-wheels
and they rest on the rails, the friction between
them, as has already been pointed out, resists their
slipping on each other, and thus enables a locomotive
to exert tractive force. Friction also resists the turning
of an axle on its journal and therefore makes the
tractive force of the locomotive necessary to move a
train of cars.
Question 359.On what does the amount of friction
depend?
Answer. The amount of friction of two bodies in
contact depends (1) UPON THE PRESSURE OF THE ONE
ON THE OTHER, AND IS INDEPENDENT OF THE AREA
OF THE SURFACES IN CONTACT; (2) ON THE NATURE
OF THE MATERIALS IN CONTACT; (3) ON THE NATURE
OF THE SUBSTANCE, SUCH AS OIL OR OTHER LUBRICANT,
WHICH IS INTERPOSED BETWEEN THEM. Thus,
a brick will slide down an inclined board as easily if
it is laid on its broadest side as it will if placed edgewise;
and if a cast iron plate, say 10 inches square,
is planed and scraped, so as to be as nearly a perfect
plane surface as it is possible to make it, it will, if
loaded with say a hundred pounds weight, slide on a
similar true surface as easily as another plate with
half as much area and loaded with the same weight.
A shaft resting against a long bearing will require
no more power to turn it than would be needed if
the bearing was short.[83]
[83] In fact, ordinarily less power is required to turn it if the bearing is
long than if it is short, the reasons for which will be explained hereafter.
Question 360.What is meant by the “co-efficient of
friction?”
Answer. It is the proportion which the resistance to
sliding motion bears to the force pressing the surfaces
together. Thus a smooth, clean and dry cast iron
plate loaded with 100 pounds will require a force of
about 15 pounds, or fifteen one-hundredths of the
weight or pressure of the plates, to slide them on
each other. The co-efficient of friction is therefore said
to be 0.15, and with any other weight or pressure on
the plates we could determine the force required to
slide them on each other by multiplying the pressure
by the co-efficient of friction. Thus, if the plates were
loaded with 250 pounds, the force required to slide
the one on the other would be equal to 250 × .15 =
37.5 pounds. The co-efficient of friction, however,
varies for different materials. Thus, while the
co-efficient of friction between two pieces of
smooth, clean and dry cast iron is 0.15, that of a
piece of brass on cast iron, under similar conditions,
is 0.22, and of two pieces of wood about 0.4.
Question 361.What is the effect of introducing some
unguent or lubricating material, such as oil, between the
surfaces in contact?
Answer. The co-efficient of friction is very much reduced
thereby. Thus the co-efficient of friction of the
cast iron plates, if their surfaces are greased with tallow,
is 0.1; if lubricated with lard 0.07, with olive oil
0.064, and with lard and plumbago 0.055, thus showing
that the amount of the friction depends very much
upon the nature of the lubricant which is used, as
well as on that of the materials in contact.
Question 362.What effect on the amount of friction
has the manner of applying the lubricating material to the
surfaces in contact?
Answer. The more perfect the lubrication the less
will be the co-efficient of friction. It has, for example,
been found by experiments made with cast iron shafts
turning on bearings of the same material that when
the lubricating material was applied so that the surfaces
were only “unctuous,” that is slightly greasy,
the co-efficient of friction was very little less than
when they were dry, that is when there was no lubricating
substance between them, and that when they
were greased “from time to time” the co-efficient was
reduced to 0.07 and 0.08; but when they were continually
oiled it averaged 0.05, and sometimes fell as
low as 0.025, showing that with the best lubrication
the friction was only one-sixth what it was when the
surfaces were only “unctuous.” Between these two
limits there is every degree of frictional resistance,
according to the condition of lubrication. This shows
how important it is that the oiling fixtures should be
kept in the most perfect condition and the utmost
care be exercised in keeping every part of a locomotive
thoroughly lubricated.
Question 363.What effect does the pressure per
square inch of the surfaces in contact have upon the
lubrication?
Answer. The tendency is, when this pressure becomes
excessive, to press out the lubricant which is
between the two surfaces, and ordinary experience
proves that the greater the weight or the force per
square inch with which two bodies are pressed together,
the greater is the difficulty of keeping them
perfectly lubricated.
Thus it is easier to keep the journals of a car well
lubricated when it is empty than when it is heavily
loaded, and the guide-bars of a locomotive are more
liable to be cut when the engine is pulling a heavy
load than with a light one.
Question 364.What effect has the velocity of the surfaces
in contact on the friction and lubrication?
Answer. With the surfaces in the same condition,
the friction is independent of the velocity of motion of
the surfaces against each other, but perfect lubrication
becomes more difficult as the velocity increases,
so that an increase of velocity will often increase indirectly
the amount of friction. Thus, taking our previous
illustrations, it is more difficult to keep the
journals of a car or engine well lubricated when running
fast than when running slow, and the same thing
is true of the guide-bars.
Question 365.What considerations should govern the
proportions of frictional bearings for locomotives and
other machines?
Answer. The dimensions to be given them should
not be determined from a consideration solely of their
resistance to rupture,[84] but they should be made so
large that the pressure they must bear will be distributed
over so much surface that the proportion
borne by each square inch will be comparatively small,
thus making good lubrication much less difficult, and
consequently reducing the co-efficient of friction.
Question 366.Is not the amount of energy required
to overcome the friction on a journal of large diameter
greater than would be required if the journal was
smaller?
Answer. If the co-efficient of friction in the two
cases is the same, undoubtedly the large journal will
require the greatest expenditure of energy to turn it,
because its periphery moves further than that of the
small one; but the advantage attributed to large
journals is that they can be lubricated more perfectly,
because their surfaces being larger the pressure is not
so great per square inch, and thus the gain from the
reduction of the co-efficient of friction is greater than
the loss attributable to the increase of the diameter of
the journal. Thus if a car journal is 3¹⁄₄ inches in
diameter × 5¹⁄₂ inches long, the available surface exposed
to friction is equal to that of a longitudinal
section of the journal, or 3¹⁄₄ × 5¹⁄₂ = 17.875 square
inches.[85] Supposing now that the journal is loaded
with 5,000 pounds, and the average co-efficient of friction
is 0.085. In one revolution of the wheel the
journal will move 0.85 of a foot, and therefore 5,000 ×
.085 = 361¹⁄₄ foot-pounds of work. If now the journal
is made, as has been proposed, 3³⁄₄ × 7 inches, then its
effective surface will be equal to 26¹⁄₄ square inches,
but the journal will move 0.98 of a foot in one revolution.
If, however, the lubrication is improved by the
increased area of the journal so that the co-efficient of
friction is reduced from 0.085 to 0.07, then the energy
consumed in one revolution will be equal to 5,000 ×
0.7 × .98 = 343 foot-pounds, or less than was consumed
with the small journals. The co-efficient of friction is
assumed, and could only be determined by experiment,
but the assumption shows how the resistance of
the large journals may be less than that of the small
ones. Of course it would be better to give the increased
bearing surface by adding to the length of the
journal, but nearly all locomotives and car journals
must be increased in diameter as well as in length
when they are enlarged, in order to have the requisite
strength to carry the loads they must bear.
[85] The reason for this is that
the effective surface of the journal A, fig.
209. which resists the pressure of the bearing, is equivalent only to the
horizontal area represented by the dotted line a. b. just as the surface
which resists the pressure inside of a boiler is equivalent to the diameter
multiplied by its length, as was explained in answer to Question 99.
Question 367.Is the law thatFRICTION IS IN PROPORTION
TO THE PRESSURE ON EACH OTHER BY THE
SURFACES OF CONTACTtrue under all circumstances?
Answer. No; there is a limit to the exactness of the
above law, when the pressure becomes so intense as to
crush or grind the parts of the bodies at and near
their surfaces of contact. At and beyond that limit
the friction increases more rapidly than the pressure;[86]
and the friction then becomes very irregular.
Question 368.In what cases is the limit referred to
probably reached?
Answer. Probably in some locomotives the pressure
of the driving-wheels on the rails is sufficient to partly
crush the latter.
Question 369.What effect has the nature of the materials
in contact on the friction?
Answer. The amount of friction and also the lubrication
is very much influenced by the nature of the
bearing surface and also by the material used as a lubricant.
Some metals, such as brass and other alloys,
are much less liable to abrasion and seem to retain
lubricants on their surfaces better than other metals,
and are therefore much used for journal and other
bearings. Some substances, especially oils, are good
lubricants, while other materials of apparently similar
nature are not. The reason why these materials possess
these properties while others are without them is
not known, and the value of any material as a lubricant,
or the degree to which another will resist friction
without abrasion, can only be tested by experiment.
PART XIX. COMBUSTION.
Question 370.What is meant by combustion?
Answer. By combustion is meant the phenomenon
ordinarily called burning, as when a piece of wood or
coal or a candle is burnt. In reality combustion is a
union of one of the “chemical elements,” oxygen, of
which the atmosphere is composed, with the elements
which constitute the fuel.
Question 371.What is meant by the term “chemical
element?”
Answer. The science of chemistry has demonstrated
that nearly all substances by which we are surrounded
are composed of certain other substances, which latter,
as far as is now known, are not compounds, and are
therefore called elementary substances, or chemical elements.
Thus the air by which we are surrounded is
composed of two gases, called nitrogen and oxygen;
water is composed of hydrogen and oxygen, and
coal chiefly of carbon and hydrogen. There are
now over sixty of these elementary substances known.
From no one of them have chemists been able to extract
any material excepting the substance itself.
These elementary substances will combine with others
so as to form what is apparently a new material, but
on weighing it it will be found that the weight of the
new material is greater than the original elementary
substance, showing that something was added to it
which effected the change.[87]
Question 372.To what fact is this combination or
combustion of elementary substances due?
Answer. It is owing to the fact—the exact reason
for which is perhaps not yet understood fully—that
the atoms of the elementary substances of which fuel
is composed, that is hydrogen and carbon, and the
atoms of oxygen, which forms part of the atmosphere
by which we are surrounded, attract each other with
great energy when they are excited into activity by
the application of heat.
Question 373.What phenomenon always attends
chemical combination of substances?
Answer. Such combination always gives out heat,
whereas their separation absorbs heat. It has further
been proved by actual experiment that the amount of
heat liberated by the chemical union of the same
quantity or number of atoms of two or more substances
is always the same, and that when, by any cause, the
atoms thus joined are separated, exactly the same
amount of heat is absorbed.[88]
Question 374.In what proportions do the elementary
substances combine with each other?
Answer. It is a law of chemistry that each of the
elementary substances combines with the others in
certain definite proportions only. These proportions
vary for the different elements, and have been determined
with great accuracy by chemists. Thus, eight
parts by weight of oxygen will combine with nitrogen
and form atmospheric air, or the same proportion of
oxygen will combine with hydrogen and form water,
or with carbon and form carbonic acid, which is the
deadly gas which accumulates at the bottom of wells.
Now oxygen always combines with other substances
in the proportion of eight parts by weight, or by some
simple multiple of eight, that is 8 × 2 = 16 parts, or
8 × 3 = 24 parts, etc. Each of the other elementary
substances also has a certain fixed proportion in which
it combines with others, and this proportion, which is
usually given by weight, is represented by a number
called its chemical equivalent. Thus 8 is the chemical
equivalent of oxygen. Carbon combines with other
elements in proportions of 6 and nitrogen in proportions
of 14, so that 6 and 14 are the chemical equivalents
of carbon and nitrogen. Now 8 parts by weight
of oxygen can be made to combine with 14 parts of
nitrogen, or 8 × 2 = 16 parts of oxygen will combine
with 14 of nitrogen, but it is impossible to make, say
12 parts of oxygen combine with 14 parts of nitrogen.
We can combine 14 × 2 = 28 parts of nitrogen with 8
parts of oxygen, but no chemical process can make
say 10 or 20 parts of nitrogen combine with 8 parts of
oxygen. If 20 parts of nitrogen are mixed with 8
parts of oxygen, then the latter will combine with 14
parts of the former, but 6 parts of nitrogen will be left,
and chemical combination will then cease.
The following table will give the chemical equivalents
of the principal elements which enter into the
process of combustion of the fuel used in locomotives:
Chemical equivalent by weight.
Oxygen
8
Nitrogen
14
Hydrogen
1
Carbon
6
Sulphur
16
Question 375.What effect do the proportions in which
elements are combined have upon the substances which are
produced by the combination?
Answer. A change in the proportions in which the
elements are combined usually alters the entire nature
of the substance, so far at least as it affects our senses.
For instance, oxygen unites chemically with nitrogen
in different proportions, forming five distinct substances,
each essentially different from the others,
thus:
14
parts
of
Nitrogen
with
8
of
Oxygen
forms
Nitrous Oxide.
14
„
„
„
„
16
„
„
„
Nitric Oxide.
14
„
„
„
„
24
„
„
„
Hyponitrous Acid.
14
„
„
„
„
32
„
„
„
Nitrous Acid.
14
„
„
„
„
40
„
„
„
Nitric Acid.
We here find the elements of the air we breathe, by
a mere change in the proportions in which they are
united, forming distinct substances, which differ from
each other as much as laughing gas (nitrous oxide) does
from that most destructive agent nitric acid, commonly
called aqua fortis.[89]
[89] Combustion of Coal and the Prevention of Smoke, by C. Wye Williams.
Question 376.What occurs when a fresh supply of
bituminous coal is thrown on a bright fire in the fire-box
of a locomotive?
Answer. The fresh coal is first heated by the fire,
and if a sufficient quantity is thrown in to prevent the
immediate formation of flame,[90] a volume of gas or
vapor, usually of a dark yellow or brown color, is given
off. The quantity evolved will be greatest when the
coal is very small. This gas or vapor is commonly
called smoke, but it does not deposit soot and in reality
is not true smoke. If a sheet of white paper be held
over the vapor as it escapes from the coal and there is
no flame, the sheet will become slowly coated with a
sticky matter of brown color difficult to remove, and
having a strong tarry or sulphurous smell; whereas
if a sheet of paper is held over smoke it will quickly
be covered with black soot. The color and smell left
on the paper in the first case are due to the tarry
matter, sulphur, and other ingredients in the gas.
Deprived of the coloring matters, the vapor is a chemical
mixture of 2 parts of hydrogen and 6 parts of
carbon, and is called carburetted hydrogen, and is
nearly the same as the colorless gas by which our
houses are lighted.[91] A similar gas is generated at
the wick of a burning candle or lamp and is consumed
in the flame. Before the gas is expelled from the fresh
coal the latter must be heated to a temperature of
about 1,200 degrees, so that if 100 pounds at a temperature
of 50 degrees is put on the fire 23,000 units
of heat will be absorbed to heat the coal.[92] Nor is this
all, as has been explained in answer to Question 38,
when any substance is vaporized a certain amount of
heat apparently disappears, which has been called the
heat of evaporation or of gasification. Average bituminous
coal contains about 80 per cent. of carbon, 5 per
cent. of hydrogen and 15 per cent. of other substances
usually regarded as impurities. When the coal is
heated up to about 1,200 degrees, the 5 per cent. of
hydrogen unites with three times its weight of carbon,
and thus 20 per cent. of the coal is converted into the
gas described. In this process a large amount of heat
is absorbed or becomes latent, as it does when water or
any other substance is converted into vapor. It will
therefore be seen that the first effect of putting fresh
coal on the fire is to cool the fire. This fact has an important
bearing on the question of combustion and
will be referred to hereafter.
[90] Usually if more than two or three shovels full are thrown in there
will be no immediate formation of flame.
[91] A Treatise on Steam Boilers, by Robert Wilson.
[92] The quantity of heat required to heat coal is only about one-fifth
that needed to heat the same weight of water to the same temperature.
Question 377.How can the process of the combustion
of the gas generated from the coal be best explained?
Answer. As this gas is substantially the same as
ordinary illuminating gas, the manner in which it
burns can perhaps be made clearer by examining the
combustion of an ordinary gas-light. As stated before,
combustion is a chemical union of the oxygen
which forms one of the elements of the air with the
hydrogen and carbon of the fuel, which, in this case,
form gas. It should be clearly kept in mind that
combustion is the result of this union, and that the
oxygen is as essential to combustion as coal or gas,
and in fact is the fuel of combustion just as much as
coal or gas is. If we were to conduct a pipe from the
external air into a vessel filled with coal gas we could
light the air and it would burn in the gas as the gas
burns in the air.
It will be noticed, however, that before either the
gas or the air will burn, they must be lighted. Air
and gas, even if mixed together in the same vessel,
will not burn unless they are lighted. This can be
done by the flame of any burning material, or with a
piece of metal heated to a very high temperature, or
by an electric spark. In other words it may be said
that the atoms of the two gases must be excited into
activity by the application of heat, that is, what is
called an igniting temperature must be communicated
to them before chemical combination will begin. The
chief feature which distinguishes combustion from
other chemical union is the circumstance that the heat
generated during the combination is sufficient to
maintain an igniting temperature, and the necessity
of doing so in order to continue the process is of very
great importance in the combustion of coal in locomotive
boilers, as will be shown hereafter.
Question 378.How does an ordinary gas-light burn
after it is lighted?
Answer. Under ordinary conditions the hydrogen,
which is the most combustible of the two elements of
which coal gas is formed, is the first to burn. This
part of the combustion forms the lower bluish part of
the flame. The combustion of the hydrogen thus
separates it from the carbon, which is then set free;
and as carbon is never found in a gaseous condition
when uncombined with other substances, it at once
assumes the form of fine soot when the hydrogen is
burned away from it. This fine soot, or pulverized
carbon, is, however, intensely heated by the combustion
of the hydrogen. Now carbon when heated to an
igniting temperature will, if brought into contact with
a sufficient quantity of oxygen, combine with it or be
burned. Each particle of carbon thus becomes a
glowing centre of radiation, throwing out its luminous
rays in every direction. The sparks last, however,
but an instant, for the next moment they are consumed
by the oxygen which is aroused to full activity
by the heat, and only a transparent gas rises from the
flame. But the same process continues; other particles
succeed, which become heated and ignited in their
turn, and it is to this combustion of the solid particles
of carbon that the light which is given out by a gas-burner
or candle is due.[93]
Question 379.Why does a gas-burner, candle or other
flame sometimes smoke?
Answer. Because the supply of oxygen is then insufficient
to consume the particles of solid carbon
which are set free and which then assume the form of
soot. This can be illustrated if we cut a hole in a
card, d d, fig. 210, so as to fit over an ordinary gas-burner,
b. If we then light the gas and place a glass
chimney, a a, over the burner and let it rest on the
card, it will be found that the flame will at once begin
to smoke, because very little air can then come in contact
with the flame, and therefore when the fine particles
of carbon are set free by the combustion of the
hydrogen, instead of being burned as they would be
if the air with its supply of oxygen were not excluded
from the flame by the chimney, they escape unconsumed
in the form of fine black powder or soot. If
we raise the chimney up from the card, as shown in
fig. 211, so as to leave enough space between them at
the bottom of the chimney to permit air to enter so as
to supply the flame with oxygen, the smoke will instantly
cease, as the particles of carbon are then consumed.
The same principle is illustrated in an ordinary
kerosene lamp. It is well known that without
a chimney the flames of nearly all such lamps smoke
intolerably, whereas with a glass chimney and the peculiarly
formed deflector which surrounds the wick
the light burns without smoke unless the wick is turned
up high. The effect of the chimney is to produce a
draft, which is thrown against the flame by the deflector,
and thus a sufficient supply of oxygen is furnished
to consume all the particles of carbon, whereas
without the draft produced by the chimney the supply
of oxygen is insufficient to ignite all the carbon, which
then escapes in the form of smoke or soot.
Fig. 212.
Fig. 213.
It must not, however, be hastily assumed that if the
flame does not give out a bright light, therefore the
combustion is not complete. As has already been
stated, the light of the gas flame is due to the presence
of burning particles of solid carbon, which is set
free by the combustion of the hydrogen with which it
is combined. After it is separated from the hydrogen
it immediately assumes a solid form. If the coal gas
is mixed with a sufficient quantity of air before it is
burned, the oxygen in the latter will be in such intimate
contact with the former that the difference of
affinity of oxygen for the carbon and hydrogen does
not come into play, and as there is enough oxygen for
all, the carbon is burnt before it is set free, and as
there are then no solid particles in the flame, there is
no light. This is illustrated by a “Bunsen burner,”
fig. 212, which is much used in chemical laboratories.
It consists of a small tube or burner, a, which is placed
inside of another larger tube b. The latter has holes,
c, c, a little below the top of the small tube. The
current of gas escaping from the small tube produces
what is called an induced current of air in the large
tube. This air enters through the holes c, c, and is
mixed with the gas in the tube b, and the mixture is
burned at d. The flame from such a burner gives
hardly any light, but the heat is intense, as is shown
if a metal wire is held in it for a few seconds, as it
will very soon glow with heat.
Question 380.What important difference is there in
the structure of the flame of a Bunsen burner and that of
an ordinary gas-burner or candle?
Answer. The gas which escapes from the mouth d of
the pipe b, fig. 212, is mixed with air, and therefore
contains within itself the elements which only need
to combine to produce combustion; whereas with an
ordinary gas-burner or candle the air comes in contact
with the flame only from the outside, or on its surface.
This is shown better perhaps in the flame of an ordinary
candle. The heat of such a flame distils a gas
from the melted tallow, which is similar in nature to
that which escapes from coal at a high temperature.
Now by observing the candle very closely it will be
seen that at the bottom close to the wick there is very
little combustion, as the gas there first escapes from
the wick and is not heated to a sufficiently high temperature
to burn freely. A little above the lowermost
part the flame is of a pale bluish color, which is due
to the combustion of the hydrogen. Above that,
where the carbon is set free, its particles glow with
heat imparted by the burning hydrogen and are then
consumed by uniting with the oxygen of the air. The
combustion occurs only at the surface of the flame,
the inside being a mass of combustible gas which cannot
burn until it in turn comes in contact with the
oxygen of the air. This can be proved by inserting
one end of a small tube, fig. 213 (a pipe stem will do),
which is open at both ends, into the flame. The combustible
gas will then escape at the other end and can
easily be lighted with a match.
It will be found that the flame from the Bunsen
burner is much more intense than that of an ordinary
candle or gas-burner. The reason of this is that combustion,
as already stated, takes place through the
whole mass of its flame, whereas an ordinary flame
burns only at its surface. Common gas-jets are therefore
arranged so that the flames will be flat, thus exposing
as much surface to the air as possible, and, as
explained in answer to Question 329, in describing
the lamps for head-lights, their burners are usually
made with a circular wick, through the centre of
which a current of air circulates. This arrangement
exposes a larger surface of the flame to the air, and
also with the aid of a chimney furnishes an abundant
supply for combustion. In stationary boilers with
long flues of a large sectional area the flame will
often extend for thirty feet, showing that while combustion
is going on only at the surface of the flame,
it takes a long time to complete the process. The
same thing is shown if a gas-burner is made with a
single round hole. The flame will then be very long
and liable to smoke at the top.
Question 381.From the preceding considerations
what may we infer to be necessary in order to consume coal
gas perfectly?
Answer. In the first place, that there must exist a certain
degree of what chemists call “molecular activity,”
which is produced by heat, or what we have called the
igniting temperature. The necessity of this is sufficiently
obvious with ordinary gas-burners, as they
must always be lighted before they will burn. Now imagine
that it was required to burn gas which was issuing
from a hundred jets, of every variety of size, in a
violent wind storm, or gusts of wind. Obviously it
would be necessary to keep a lighted torch all the time
to relight those which would be blown out. The gas
in a locomotive fire-box is in reality burnt in a storm
of wind more violent than any natural one. It is
therefore necessary to be constantly ready to relight
the streams of gas which the faintest breath would
extinguish, or those of larger volume which have absorbed
a great deal of heat and thus reduced the temperature
at the time and place of their birth, when they
assumed the gaseous form, as was explained in answer
to Question 376. To relight them with certainty it is
necessary to keep a constant temperature in the fire-box
high enough to ignite the gas which escapes or is
distilled from the coal.
Second. That the chemical change in combustion
consists simply in the union of the elements burned
with the oxygen of the air; and therefore, to burn the
gas perfectly, without smoke or waste, enough air must
be furnished to supply all the oxygen which will combine
with the fuel.
Third. That the air must be mixed with the gas,
otherwise combustion will occur only at the surface
of the flame, and will therefore be so slow that much
of the gas will escape unconsumed.
It must be clearly kept in mind that no one or two
of these requirements alone, without the third, will
burn coal perfectly. What is needed is all three in
combination. A very common error is to suppose that
passing smoke over a hot fire, or in other words, maintaining
an igniting temperature, will alone effect perfect
combustion; or that if a sufficient supply of air
is admitted, without an igniting temperature in the fire-box,
the fuel will be burnt completely. Neither of them
will accomplish the object alone, and the gas and air
must at the same time be thoroughly mixed with the
burning gas in the fire-box.
Question 382.What substances are produced by the
combustion of coal gas?
Answer. The hydrogen of coal gas unites during
combustion with oxygen in the proportion, as indicated
by their chemical equivalents, of 1 part by weight
of hydrogen with 8 parts of oxygen, the product of
which is water. Of course at the high temperature
at which the gases combine or burn the water is produced
in the form of steam. That water or steam is one
of the products of combustion is shown every cold evening,
when the insides of shop show-windows are covered
with moisture, which is due to the steam that is given
off by the burning gas-lights or lamps inside, and is
then condensed against the cold glass.
Carbon combines with oxygen in two proportions:
first, 6 parts of the former will unite with 8 of the
latter, forming what is called carbonic oxide; or 6 parts
of carbon will combine with 16 parts of oxygen, forming
carbonic acid gas or carbonic dioxide, as it is called
in some of the new books on chemistry. It is probable
that the former compound, that is carbonic oxide,
is never or very rarely formed in the flame of coal gas;
but, as will be seen hereafter, is a very common and
wasteful product of the combustion of the solid portion
of the coal which is left after the gas is expelled from
it. When there is not enough oxygen for the perfect
combustion of the carbon in the flame, it smokes, and
the carbon escapes in the form of soot. This, as will
be shown, may in a locomotive fire-box help to form
carbonic oxide after it leaves the flame.
Question 383.What remains in the coal after all the
gas is expelled by heat?
Answer. What remains is ordinarily called coke,
which, with the exception of some incombustible substances,
such as sand, ashes and cinders, which the coal
contains, is nearly pure carbon.
Question 384.What is the chemical process of the
combustion of coke?
Answer. The solid carbon of the coke when raised
to an igniting temperature; or, in other words, on
being lighted, unites with the oxygen in one of the two
proportions already given; that is, if the supply of oxygen
is sufficient, 6 parts of the carbon of the coke
unite with 16 parts of oxygen, forming carbonic acid
gas, or carbonic dioxide. If, however, the layer of
fuel on the grates is thick, or the supply of air is comparatively
small, there will not be enough oxygen to
supply 16 parts of the latter to each 6 parts of the
carbon, so that when that occurs, instead of combining
in that proportion, and thus forming carbonic
dioxide, 8 parts of oxygen will unite with 6 parts of
carbon and form carbonic oxide. Now it should be
carefully kept in mind that the heat of combustion is
due to the union, or, as it is sometimes expressed, it is
the clashing together of the molecules of the two elements
which unite. If, therefore, only half the quantity
of oxygen unites with 6 parts of carbon, evidently
there will be less heat evolved than there would
be if twice that amount of oxygen combined with the
carbon. From carefully made experiments it was
found that the total heat of the combustion of one
pound of carbon when converted into carbonic oxide
was 4,400 units, whereas when it was converted into
carbonic dioxide 14,500 units were given out. It will
thus be seen that it is extremely wasteful to burn coal
without a sufficient supply of air to produce carbonic
dioxide. The danger of waste from this cause is also
increased by the fact that carbonic oxide is colorless
and odorless, and therefore its production is not apparent,
especially as most persons have the impression
that when there is no smoke from a fire combustion is
then complete. It burns with a blue or yellowish flame
when air is admitted into the fire-box, and its presence
can often be detected by these phenomena when the
furnace door is opened.
Question 385.How can the requisite quantity of air
be supplied to the fire in a locomotive fire-box?
Answer. It is done in two ways: one is to keep but
little coal on the grates, or in the phraseology of firemen,
to “carry a light fire.” The other method is to
admit fresh air above the fire. If the latter plan is
adopted when the supply of air through the grates is
insufficient for perfect combustion, the carbonic oxide
will unite with the oxygen of the air above the fire,
and thus a second combustion will take place, the
product of which will be carbonic dioxide. It must
be kept in mind, however, that not only must there be
enough air supplied to the fire to consume the coke,
but the gases which are distilled from the coal must
also be supplied with oxygen in order to effect their
perfect combustion. Even if enough air is admitted
to consume the coke perfectly, if the carbonic dioxide
thus formed is mixed with large quantities of smoke
above the fire, the solid carbon or soot of the smoke
may then combine with the dioxide and thus form carbonic
oxide, if there is not enough fresh air present to
furnish the requisite oxygen for the carbon in the
smoke. A very common error is to suppose that smoke
can be burned by passing it over or through a very
hot fire. The smoke may thus be made invisible, it
is true, but it does not therefore follow that it is perfectly
consumed.
Question 386.Is it possible to admit too much air
into the fire-box of a locomotive?
Answer. Yes; probably all the air that is admitted
which is not necessary for combustion, or, in other
words, the oxygen of which does not combine with the
fuel, instead of increasing diminishes the amount of
water converted into steam. It does this in two
ways; first, by reducing the temperature of the gases
in contact with the heating surfaces, and second, by
increasing the volume or quantity of the gases which
must pass through the tubes. Heat is transmitted
through the heating surface of a boiler in proportion
to the difference of the temperature of the products of
combustion on one side and the water on the other.[94]
Thus, if the temperature of the water on one side
is 250 degrees, and the hot gases on the other is 500,
there will be only half as much heat transmitted to
the water in a given time as there would be if the
gases had a temperature of 750 degrees. If the volume
of gases is doubled by the admission of too much
air, then obviously in order to pass through the tubes
they must move at double the velocity, so that not
only is their temperature diminished, but the time
they are in contact with the heating surface is diminished
in like proportion. This is shown by the effect
of opening the furnace door, or of allowing the fire to
burn away so that portions of the grate are left uncovered.
The volume of cold air which will in either
of these cases enter the fire-box will be so great that
the pressure of the steam in the boiler will begin to
fall at once.
[94] This law is perhaps not absolutely correct, but is near enough for
our present illustration.
Question 387.What determines the amount of air
which must be admitted to the fire-box of a locomotive to
effect perfect combustion?
Answer. This depends chiefly upon the rate of combustion,
that is, the number of pounds of coal consumed
per hour on each square foot of grate surface.
Of course if 100 pounds is burnt it will require twice
the supply of air that would be needed if only 50
pounds were burnt.
Question 388.How should the air be admitted so as
to burn the coal perfectly?
Answer. In burning bituminous coal it has been
shown that there are two distinct bodies to be dealt
with, the one coke, a solid, the other coal gas, which is
of course a gaseous body. The combustion of each of
these is necessarily a distinct process. If the requisite
quantity of air is supplied to the burning coke, or
solid portion of the coal, it will, as has been shown,
be converted into carbonic dioxide, and thus be perfectly
consumed. If the supply of air is insufficient,
the product of the combustion will be carbonic oxide,
which is very wasteful. If, for example, there is a
thick layer of coke on the grate, the air will enter and
unite with the lower layer of coal and form carbonic
dioxide, but as it rises there will not be enough air to
supply oxygen to the carbon, and another equivalent
of the latter will therefore combine with the carbonic
dioxide and form carbonic oxide. It is evident,
though, that the thinner the fire, the easier it is for
air to pass through it, and consequently the greater
will be the quantity which will enter the fire-box.
Nothing would seem easier then than to regulate the
thickness of the fire on the grates so that just the
needed amount of air would pass through it. If coke
alone was to be burned, undoubtedly very perfect combustion
would be (and has been) effected in this way,
but if a charge of fresh coal, say 100 pounds, is thrown
on the fire, the coal gas is very soon generated and escapes
into the fire-box. This gas needs an additional
amount of air for its combustion. It would seem that
this could be supplied by reducing the thickness of
the fire still further, so that more air would pass
through it than was needed for the combustion of the
coke alone. If this was done then too much air would
pass through the coke after the gases had all escaped
from the fresh coal and were burned. Besides, the
passage of the air would be the most restricted after
the fresh charge had been put on the fire, just at the
time when the most is needed. This difficulty might
be overcome if a constant supply of fresh coal just
equal to that consumed were kept on the fire all the
time, and the thickness of fuel on the grates was then
regulated so as to admit just air enough for the combustion
of the coke and also that of the gases, the
production of which would then be uniform. An approximation
to this method of feeding the fire is, in
fact, what is aimed at on most locomotives, and probably
the best practical results are produced by that
method.
Two difficulties are, however, encountered in this
method. In the first place it is impossible to feed a
fire continuously with a shovel. There will be intervals
between the charges which are thrown in, so that
the supply is not uniform, even if the charges do not
consist of more than a portion of a shovel-full at a
time; and if the fire was fed in this way as uniformly
as possible it would then be necessary to open the furnace
door every time fresh coal was put on the fire,
and so much cold air would thus be admitted that
more would be lost by lowering the temperature of the
boiler than would be gained by the improved combustion.
Another difficulty also is encountered in this method
of burning coal in locomotives. In order to admit enough
air through the fire it is necessary to keep the latter so
thin on the grates that the violent draft produced by
the blast lifts the coal from the grate-bars and carries
the lighter particles through the flues unconsumed.
It is thus extremely difficult to keep the grate uniformly
covered with coal, and if it is not, the air will
enter in irregular and rapid streams or masses through
the uncovered parts, and at the very time when it
should be there most restricted. Such a state of things
at once bids defiance to all regulation or control, so
that it is found almost uniformly that firemen of locomotives
keep enough coal on the grates to avoid the
danger of “losing their fire,” as they express it; that
is, having all the burning coal drawn through the
tubes by the blast. Now, on the control of the supply
of air depends all that human skill can do in effecting
perfect combustion and economy; and unless the supply
of fuel and the quantity on the bars can be regulated,
it will be impossible to control the admission of the
air.[95]
Another method of feeding locomotive boilers is to
pile up the coal in the back part in a thick layer and
slope it downward towards the front, so that there is a
comparatively thin fire in front. The mass piled up
at the door becomes converted into coke, and the production
of gas from the coal is more gradual and uniform
than it is when only a small quantity is thrown
in at a time, and therefore a more uniform supply of
air is needed for its combustion. But it is apparent
that very little air can pass through the thick heap of
coal at the back part of the fire-box, and that therefore
all, or nearly all the air which enters it must
come in through a comparatively small portion of the
grate. It will of course be difficult to admit the
requisite quantity, for the reasons already stated.
It is consequently apparent that it is practically impossible
to admit enough air through the grates to
effect a constantly perfect combustion of bituminous
coal. It is, therefore, necessary to admit a portion of
the air above the fire. In doing this, however, in order
to effect perfect combustion the air thus admitted
must be thoroughly mixed with the gases, and in order
to be able to enter into chemical combination, or in
other words, to burn, the gases must combine with the
air at an igniting temperature. If too much air is
admitted, it will reduce the temperature in the fire-box
so much that the gases will not ignite; or, if it is
admitted in strong currents, the air and the gases will
flow side by side like the currents of two streams of
water, the one muddy and the other clear, which, as
is well known, mingle very slowly. Besides, if a hot
stream of gas encounters a strong stream of cold air
and comes in contact with it only at its surface, the
latter will be cooled down below the igniting temperature;
whereas if the two had been intimately mixed
in the right proportion, the whole mixture would have
been hot enough to burn. It is therefore of the utmost
importance that the air which is admitted above
the fire should enter the fire-box in many small jets.
None of the openings for its admission should exceed
¹⁄₂ inch in diameter. With the violent draft in a locomotive
fire-box there is an extremely brief period of
time for chemical combination to take place after the
gases are expelled from the coal and before they are
hurried into the tubes. As the chemical action between
the gases and the oxygen can only take place
when the two are in intimate contact, too much pains
cannot be taken to distribute the currents of admitted
air and thus mix them with the combustible gases.
In many cases means are adopted to delay the air and
the gases in the fire-box so as to give them time for
chemical combination or combustion before entering
the tubes.
Question 389.Does any combustion take place after
the gases enter the tubes?
Answer. Very little; as the flames are extinguished
soon after they enter.
Question 390.Why are the flames extinguished in
the tubes?
Answer. They are then in contact with large quantities
of incombustible gas and beyond the reach of a
supply of air; besides, the temperature of the tubes
which are surrounded with water is so low that the
flame is soon cooled down below an igniting temperature.
Question 391.What temperature is necessary to ignite
coal gas or produce flame?
Answer. A temperature considerably hotter than red-hot
iron is needed, as can easily be shown by the fact
that a gas-light can not be ignited with a red-hot poker.
Question 392.Are there any parts of the fire-box
where the temperature is probably below the igniting
point?
Answer. Yes; along the sides and ends near the
plates, which are covered with water on the opposite
side. At these points the coal is usually “dead” or
incandescent, as it remains at too low a temperature
to burn. For this reason, in some cases a space of
from 8 to 12 inches on each side and still more at the
ends of the grates, is made of solid plates, without any
openings, and therefore called “dead-grates,” so that
no cold air can enter at those points. These plates
are made sloping downwards from the sides towards
the centre of the fire-box, so that the coal which falls
on them and is thus coked, can easily be raked towards
the middle of the fire. This arrangement of dead
plates often improves the combustion and results in
greater economy of fuel. The reduction of the area of
the openings between the grate-bars can usually be
compensated by making the bars narrower or the
spaces between them wider.
Question 393.What should be the condition of the
coal when it is put on the fire?
Answer. It is true of the coal as well as of the gases
that the chemical action between it and the oxygen
can only take place when the two are in intimate
contact, and therefore the rapidity and completeness
of combustion and intensity of heat will be increased
by increasing the number of points of contact, or by
reducing the size of the fuel. The coal should therefore
be broken up, but not so small as to fall between
the grate-bars or be carried out of the fire-box by
the blast.
Question 394.What amount of air must be admitted
to the fire to effect perfect combustion?
Answer. It was stated that average bituminous coal
contains about 80 per cent. carbon, 5 per cent. of hydrogen
and 15 per cent. of other substances. As a
large proportion of the latter are incombustible, we
will confine ourselves for the present to the consideration
of the combustion of the hydrogen and carbon
alone.
The hydrogen, as has been explained, unites with
oxygen in the proportion by weight of 1 part of the
former to 8 parts of the latter, and the product of this
union is water, or steam. As 36 parts of air contain
only 8 of oxygen, IN ORDER TO BURN THE HYDROGEN
IT MUST BE SUPPLIED WITH 36 TIMES ITS WEIGHT OF
AIR.
In order to burn the carbon perfectly it must, as
has been explained, be converted into carbonic dioxide,
which consists of 6 parts of carbon and 16 of oxygen;
and as air consists of 28 parts of nitrogen to every 8
of oxygen, we must furnish 72 parts of air to every 6
of carbon, or, in other words, CARBON NEEDS 12 TIMES
ITS WEIGHT OF AIR FOR ITS PERFECT COMBUSTION.
Every pound of average bituminous coal therefore
requires 1.8 lbs. of air to burn its hydrogen, and 9.6
lbs. for the carbon, or 11.4 for both. As a portion of
the other substances of which coal is composed, besides
the oxygen and hydrogen, which others have been
classed as impurities, are combustible, there will be no
material error if we estimate the amount of air required
for the combustion of bituminous coal at 12
POUNDS PER POUND OF FUEL. As each cubic foot of
air weighs 0.08072 lb., 12 pounds will be equal to
120.08072 = 148.6 cubic feet of air,
or for the sake of even figures and a quantity which
can easily be remembered, we will say 150 CUBIC FEET
OF AIR ARE NEEDED FOR THE COMBUSTION OF EACH
POUND OF COAL. This is the theoretical quantity of
air which is needed for combustion. Now, unfortunately,
the process of combustion in the fire-boxes of
locomotives is one in which any very exact combination
of the substances which unite is not possible with
the appliances which are now employed. If, therefore,
we admitted the exact amount of air given above,
while some portions of the fire where combustion was
not very active might have more air than is needed,
other portions would have too little; and if the air is
not very thoroughly mixed, the flame and burning
coal may be surrounded with the products of combustion,
which would exclude the air and thus reduce
its effect upon the fire. For this reason, besides the
air required to furnish the oxygen necessary for the
complete combustion of the fuel, it is also necessary
to furnish an additional quantity of air for the dilution
of the gaseous products of combustion, which would
otherwise prevent the free access of air to the fuel.
The more minute the division and the greater the
velocity with which the air rushes among the fuel, the
smaller is the additional quantity of air required for
dilution. In locomotive boilers, although this quantity
has not been exactly ascertained, there is reason
to believe that it may on an average be estimated at
about one-half of the air required for combustion.[96]
We would therefore have as the quantity of air needed
for combustion
150 + 1502 = 225 cubic feet.
This estimate is roughly made, but it is the nearest
approximation at present attainable. It is probable
that the supply of air required for dilution varies considerably
in different arrangements of the fire-box and
for different kinds of fuel, and it is possible that by
admitting the air for combustion in small enough jets,
and deflecting the currents of smoke and gases so as
to cause them to mingle with the air, the quantity required
for dilution might be reduced below that indicated
by the above calculation. Undoubtedly all the
air which is admitted into the fire-box which does not
combine with the chemical elements of the fuel lessens
the amount of steam generated in the boiler, both with
reference to time, that is to say per minute, and to
fuel, that is per pound of coal consumed. But with
the present locomotive boiler it is simply a choice of
two evils. If no more air is admitted than theory indicates
to be needed for combustion, then, owing to
the imperfect means which are usually employed to
cause the air and fuel to combine, a portion of the latter
will escape unconsumed; and if more air is admitted,
the temperature of the products of combustion is
lowered and their volume increased, the evils of which
have already been pointed out. It therefore becomes
a matter in which we are obliged to consult experience
and determine by experiment what amount of air
it is necessary to admit to the fuel to produce the most
economical results.
Question 395.What proportion of the air should be
admitted through the grate, and how much above the fire?
Answer. This, too, is a question which can probably
be answered best by consulting experience. The relative
quantity of air required above and below the fire
depends very much on the nature of the fuel. Coal
which “runs together” or cakes very much or has a
great deal of clinker in it, doubtless, will need more air
above the fire than other coal which is said to be
“dryer,” for the reason that it will be found impossible
to admit so much air through the caking coal in
the grate as through the other kind. An idea of the
relative quantity which should be admitted above and
below the fire may be found if we know how much air
is needed to burn the solid carbon or coke which is
left after the gas is expelled from it, and how much
for the gas itself. The gas which is expelled from a
pound of coal consists of about 0.05 lb. of hydrogen
and 0.15 lb. of carbon. Now, it has been shown that
hydrogen requires 36 times its weight of air to burn
it perfectly, so that 0.05 lb. would need 0.05 × 36 =
1.8 lbs.; and carbon requires 12 times its weight of
air, so that for 0.15 lb. of carbon 0.15 × 12 = 1.8 lbs.
is needed, so that for both 3.6 lbs. of air is required
for perfect combustion. As has been shown, 12 lbs. is
needed to consume the whole of the fuel, so that 30
per cent. of the whole supply is required for the combustion
of the gas alone. If this is diluted in the
same proportion as that required for the combustion
of the carbon, and it probably should be even more
so, we would have 30 per cent. of 225 = 67.5 cubic
feet of air required for the combustion of the gas. It
is certain, however, that the solid coke on the grates is
not perfectly consumed, or, in other words, converted
into carbonic dioxide, especially when the layer of
it on the grates is very thick. When this is the case
the air coming in contact with the lower layer of coke
forms carbonic dioxide, but as it rises through the
burning coke another equivalent of carbon unites
with the carbonic dioxide, and thus forms carbonic
oxide. If, now, enough air is admitted above the fire,
this carbonic oxide will combine with it, and, as has
been explained before, a second combustion will take
place if there is time and opportunity for combination
before the gases enter the flues. It is therefore probable
that more than 30 per cent. of the whole supply
of air should be admitted above the fire. It is at any
rate best to provide the means for admitting more, and
also appliances for regulating the supply, so that it can
be governed as experience may indicate to be best.
Question 396.Is it not possible by enlarging the grate
to admit enough air to the fire to produce perfect combustion?
Answer. Yes; when no air is admitted above the
fire, large grates are found to produce the best combustion.
But while it is true that the same amount of
heat will be produced by the union of each equivalent
of oxygen and fuel, yet if we can force more air and
fuel to unite in the same place, a higher temperature
is produced in that place, just as a fire in a blacksmith’s
forge is hotter because of the forced blast than that in
an ordinary stove, or a smelting furnace than a parlor
grate. If, then, we can concentrate the draft in the fire
of a locomotive, we secure a greater intensity of combustion;
and when the air is urged against the solid carbon
with considerable force, it comes in contact with every
point of its surface, and therefore less dilution of the air
is needed, and consequently the products of combustion
have a higher temperature; and, as has been explained,
a larger proportion of the heat is then transferred
to the water than if the temperature is lower
and the volume greater.
Intensity of combustion also has the effect of maintaining
an igniting temperature; whereas, if the same
amount of fuel is burned slowly, its heat may not be
high enough to ignite the gases as they are produced.
It is desirable, however, to have all the space that
is possible in the fire-box, so as to give room for the
mixing of the gases; but with a large fire-box and
large grate a decided improvement and economy will
often result by diminishing the effective area of the
grate by covering a part of it with dead plates, but at
the same time making provision for the admission of
air above the fire.
Question 397.What is meant by the “Total Heat
of Combustion?”
Answer. It is the number of units of heat given out
by the combustion of a given quantity (usually a pound)
of fuel.
Question 398.How is this determined?
Answer. The heat given out by the combustion of
one pound of the chemical elements of which coal is
composed has been determined by experiment, and
from such data, knowing the substances of which fuel
is composed, we can determine the amount of heat
which would be developed if they were each perfectly
consumed. Thus the total heat of combustion of one
pound of hydrogen is 62,032 units, and of the same
quantity of carbon 14,500 units.[97] Therefore, if a
pound of coal contains 5 per cent. of hydrogen, the
heat given out by the combustion of that element will
be 62,032 × 0.05 = 3,101.60 units, and if it has 80 per
cent. of carbon, the combustion of the latter would develop
14,500 × 0.80 = 11,600 units, so that the total
heat of the combustion of these two elements would be
3,101.6 + 11,600 = 14,701.6 units. It was shown in
answer to Question 40 that it required 1,213.4 units
of heat to convert water at zero to steam of 100 pounds
pressure. As steam is usually generated from water
at a temperature of about 60 degrees, the total heat
required to convert it into steam of 100 pounds pressure
would be 1,213.4 - 60 = 1,153.4 units. A pound of
average bituminous coal, therefore, contains heat
enough to convert 12¹⁄₄ lbs. of water into steam of
100 lbs. absolute pressure. Ordinarily only about half
that amount of water is evaporated in locomotive
boilers per pound of fuel.
[97] The experiments which have been made to determine these amounts
do not agree exactly, but those given are thought to be the most trustworthy.
Question 399.What are the chief causes of this waste
of heat?
Answer. It is due, first, to the waste of unburnt fuel
in the solid state. This occurs when fuel which is
very fine falls through the grates, or is carried through
the tubes and out of the stack in the form of cinders.[98]
[98] It should be remarked here that some and perhaps most of the cinders
which are carried out of the stack are not combustible but are composed
of the same materials that form clinkers on the grate.
Second, to the waste of unburnt fuel in the gaseous
or smoky state. The method of preventing this waste
by a sufficient supply and proper distribution of air has
been explained in the answer to preceding questions.
Third, to the waste or loss of heat in the hot gases
which escape up the chimney or smoke stack. The
temperature of the fire in a locomotive fire-box in a
state of active combustion is probably from 3,000 to
4,000 degrees. This heat is in part radiated and conducted
to the heating surface of the fire-box, and it is
found that more water is evaporated by this portion
of the heating surface in proportion to its area than
by any other in the boiler. The gases when they
enter the tubes transmit a portion of their heat to the
surfaces with which they are first in contact. The
amount of heat thus transmitted, as has been stated,
is in proportion to the difference in temperature of the
gases inside the tubes and that of the water outside.
After passing over the part of the tube with which
the gases are first in contact, they then arrive at another
portion of the tube surface with a diminished
temperature, and the rate of conduction is therefore diminished;
so that each successive equal portion of the
heating surface transmits a less and less quantity of
heat, until the hot air at last leaves the heating surface
and escapes up the chimney with a certain remaining
excess of temperature above that of the water
in the boiler, the heat corresponding to which excess
is wasted.[99] It is, therefore, desirable to extract as
much heat as possible from the gases before they escape
from the tubes. Now it will be impossible to
heat the water outside of the tubes hotter than the
gases inside. When the temperature of the water is
equal to that of the gases, no more heat will be transmitted
from one to the other. If the temperature of
the water is 350 degrees, that of the gases in the tubes
will never be any lower, but will escape into the
smoke-box with not less than that amount of heat.
If, however, the cold water is introduced at the front
end of the tubes, so that the surface with which the
gases are last in contact has a temperature considerably
lower than 350, then an additional amount of heat
will be transmitted before they escape. It is, therefore,
important that the cold feed-water should be admitted
near the front end of the boiler, so that the
products of combustion will be in contact with the
coldest part of the heating surface last, and thus give
out as much of their heat as possible before they escape.
As a matter of fact, the gases escape at a much
higher temperature. Experiments made by the writer
showed that the temperature in the smoke-box of a
locomotive when first starting was 270 degrees, and
when working at its maximum capacity on a steep
grade and with a heavy train it was as high as 675
degrees. The average temperature while running was,
in three trials on different parts of the road, as follows:
In making these experiments a record was made of
the indications of a pyrometer and of the steam gauge
once every minute while the engine was running. The
distance run was 19 miles for the first experiment, 13
for the second and 6 for the third, with 30 loaded
freight cars in the train. The last experiment was
made while the engine was working on a heavy grade
and very nearly up to its maximum capacity.
It will thus be seen that a great deal of heat is
wasted by escaping up the chimney.
Fourth, by external radiation from the boiler. This
occurs chiefly from the fact that it is not sufficiently
well protected or covered with non-conducting material.
The practice, or rather the neglect, of not covering
the outside of the fire-box with lagging doubtless
causes a very considerable loss of heat by radiation
and convection from the hot boiler plates.
Question 400.What is the ordinary form of fire-box
employed for burning bituminous coal?
Answer. It is that represented in plate II and figs.
41 and 44, and is simply a rectangular box, and for
that reason it is called a plain fire-box. Sometimes
provision is made for admitting air into such fire-boxes
through hollow or rather tubular stay-bolts,
which are put into the sides and front. In most cases,
too, the fire-box door has perforations for admitting air.
Fig. 214. Scale ³⁄₈ in. = 1 foot.
Question 401.What other appliances are used for
burning bituminous coal?
Answer. The most common appliance which is added
to the plain fire-box is what is called a fire-brick arch.
This is shown in fig. 214. B C is the arch which,
as its name implies, is formed of fire-brick and extends
backward and upward from a point in the tube-sheet
below the tubes. In order to be self-supporting it is
built in the form of an arch, the two sides of the fire-box
acting as abutments for its support. The engraving
represents with sufficient clearness the direction
of the flames and smoke. These must take a more
circuitous “run,” as it is called, after leaving the fire,
in order to reach the tubes. Time is thus given for
the gases to combine and combustion to take place.
The fire-brick becomes heated, and thus to some extent
prevents the gases from being cooled down below
an igniting temperature by contact with the cold surface
of the fire-box before combustion is complete.
The fire-brick, however, soon burns out, and must be
replaced, but owing to its cheapness and the ease
with which it can be removed, this does not make a
serious objection to its use. Air is nearly always admitted
above the fire when the brick arch is used,
either by tubular stay-bolts, a, a, a, or perforations in
the door, or both.
Fig. 215. Scale ³⁄₈ in. = 1 foot.
In order to avoid the inconvenience and expense of
replacing the fire-brick arch, what is known as the
“Jauriet water-table” has been extensively used on
some roads. This is the invention of Mr. C. F. Jauriet
and is represented in fig. 215, and consists of a
flat “table,” B C, formed of two boiler plates placed
about 4¹⁄₂ in. apart, with the space between filled with
water. The two plates are stayed with ordinary stay-bolts
in the same way as the sides of the fire-box. The
form of the water-table is similar to that of the fire-brick,
excepting that it is not arched, this form not being
necessary, as the plates are riveted to the sides of the
fire-box. Air is admitted above the fire both by hollow
stay-bolts and holes in the door, as shown at A.
Tubes, f, are put into the front and lower portion of
the water-table to allow the ashes and cinders, which
would otherwise be deposited above, to fall down on
the grates.
Fig. 216.
When air is admitted at the furnace door of an ordinary
fire-box, it is very apt to rush directly into the
tubes without mingling with the gases. It was found
by some of the firemen on English railroads that by
placing a shovel over the top of the furnace door, the
current of air which entered could thus be deflected
downward, and in this way smoke could be almost entirely
prevented. This led to the adoption of a hood
or deflector, A, fig. 216, which is made of sheet iron and
is placed over the fire-box door and is arranged with
a lever, B, so that it can be raised in order to be out
of the way when coal is thrown on the fire. It is suspended
from a hook, C, from which it can easily be
detached and taken out for repairs. This is frequently
necessary, as the intense heat of the fire-box burns
away the sheet iron of which it is made very rapidly.
It can be made of old boiler plate, so that the expense
of renewal is very slight. When this plan is used,
a double sliding door, shown in fig. 217, is commonly
used with it. These doors are opened by the levers f
d; and e g, which are all connected together. With
these sliding doors the opening for the admission of
air can easily be regulated, and the opening through
which the lever, B, is attached to the deflector, A, can
be arranged more conveniently than with a swinging
door. This plan has been employed by the Rogers
Locomotive Works.
Fig. 217.
Scale ³⁄₈ in. = 1 foot.
Another plan of fire-box, which was designed and
patented by Mr. William Buchanan, Master Mechanic
of the Hudson River Railroad, and used extensively
on that line, is shown in fig. 218. This consists of a
water-table, but it extends completely across the fire-box
from the tube sheet to the back-plate, thus dividing
the fire-box into two compartments, M and N. In
order to afford communication from the lower one to
the upper one a round hole, D, about 24 in. in diameter,
is put in the water-table in the position shown.
It will thus be seen that all the currents of gas, smoke
and air must unite in passing through this opening,
and are thus brought into close contact with each
other. After they enter the upper chamber and before
they enter the tubes, there is room and time for combustion.
The position of the lower side of the table,
it will be seen, is similar to that of the deflector shown
in fig. 216, so that it acts in somewhat the same way,
by directing the currents of air, which enter through
the furnace door, downward on the fire.
Fig. 218. Scale ³⁄₈ in. = 1 foot.
Question 402.How do these different plans operate?
Answer. They will all burn coal more perfectly, and
therefore more economically, if they are carefully and
skillfully managed, than is possible in ordinary plain
fire-boxes; but it is probable that more economy in the
consumption of coal would result from the improvement
of the practice and knowledge of firemen than
can be expected from the use of any of the appliances
described, if they are used without care, or knowledge
of the principles of combustion.
Question 403.In what respect does anthracite coal
differ from bituminous?
Answer. It differs chiefly in the fact that it contains
a much larger proportion of carbon and less of hydrogen,
and in the fact that it consequently gives off very
little or no coal gas. Its combustion is therefore more
simple than that of bituminous coal, as there is very
little else than solid carbon to burn.
Question 404.In what kind of a fire-box is anthracite
usually burned?
Answer. It is usually burned in a very long grate,
and as the heat is very intense, the grate-bars are
usually made of iron tubes, through which a current of
water circulates, so as to prevent them from melting.
Question 405.Is it important to admit air above an
anthracite fire to facilitate combustion?
Answer. As there are no gases to be burned, it is
not so important as it is with bituminous coal, but if
the layer of anthracite on the grates is very thick, it
will be impossible to get enough air through the coal
to convert all the carbon into carbonic dioxide, and the
carbon and oxygen will therefore unite so as to form
carbonic oxide. If air is admitted above the fire, as has
already been explained, another equivalent of oxygen
will unite with the carbonic oxide, and a second combustion
will then take place above the fire, and the carbonic
oxide will thus be converted into carbonic dioxide.
If, under these circumstances, no air was admitted
above the fire, the second combustion would not occur,
and all the heat produced thereby would be lost.
Question 406.How can we determine the relative
value of different kinds of fuel for use in locomotives?
Answer. This can only be determined satisfactorily
by actual experiment. The chemical composition, excepting
so far as it indicates the presence of deleterious
substances, such as sulphur, ashes, clinkers, etc.,
affords but little assistance in determining the value
of fuel. Nearly the same quantities of elements in different
fuels may arrange themselves, before and during
combustion, so as to produce very different series of
compounds. It is true that the composition of coal
gives us some indication of its heat-producing capacity,
but the extent to which that capacity can be converted
into actual steam in locomotive boilers, depends to a
very great extent upon the conditions under which the
fuel is burned. It should also be remembered that
the rapidity with which steam can be generated is a
very important matter in locomotive practice. Whether
a heavy freight train can be taken up a given grade,
or a fast express make time, often depends upon the
amount of steam which can be generated by the fuel
in each second of time that the boiler is worked to its
maximum capacity. Therefore any appliance for improving
combustion, which reduces the quantity of
steam which can be generated by the boiler in a given
time, is quite sure to fall into disuse or be abandoned.
It is of course often necessary to adapt the appliances
for burning fuel to the fuel itself; and when a poor
quality of the latter must be used, more boiler capacity
must be given than is needed to do the same
work with better fuel.
The table in the appendix will no doubt be valuable
as indicating the properties and relative value of several
different kinds of fuel used in this country. The table is
copied from a report made to the Navy Department of
the United States by Professor Walter B. Johnson in
1844, and the conclusions are deduced from a series of
very elaborate experiments made for the Navy Department.
This report furnishes the most full and reliable
data regarding the value of American fuel thus
far (1874) published; but it contains little or no information
concerning the fuels which are now used on
railroads in our Western States. The first eight specimens
of coal given in the table are anthracite; all the
rest are bituminous coals.
PART XX. THE RESISTANCE OF TRAINS.
Question 407.What is meant by the resistance of
trains or cars?
Answer. It is the power required to move them on
the track. Thus if a rope, fig. 219, was attached to a
car at one end, and the other passed over a pulley, a,
and a sufficiently heavy weight, W, was hung on the end
of the rope, it would move the car. The weight W
would then be equal to the resistance of the car.
Fig. 219.
Question 408.How can the resistance of cars under
different circumstances be determined?
Answer. It has been found that it takes a force of
about 6 lbs. per ton (of 2,000 lbs.) to move a car slowly
on a level and straight track after it is started. That is,
if a car weighs 20 tons and a rope, fig. 219, is attached
to it at one end and the other passed over a pulley, a,
with a weight, W, suspended to it, it will require a
weight equal to 20 × 6 = 120 lbs. to keep the car
moving slowly. If two cars of the above weight were
coupled together, it would require twice 120 or 240
lbs., and if three were attached to each other, three
times 120, or 360 lbs., and so on. In other words,
MULTIPLYING THE TOTAL WEIGHT OF THE CARS IN
TONS (OF 2,000 LBS.) BY 6 WILL GIVE US THEIR RESISTANCE,
OR THE FORCE REQUIRED TO KEEP THEM
MOVING ON A LEVEL AND STRAIGHT TRACK AT A SLOW
SPEED AFTER THEY ARE STARTED. The resistance is
represented by the weight above, and the locomotive
must exert a force equal to that weight to keep the
train moving. As the speed increases the resistance
increases, as is shown by the following table. It
should be stated here, however, that our knowledge
regarding this whole subject of the resistance of American
cars and trains is exceedingly inaccurate and imperfect,
and the data given in the books are nearly all
based on experiments made in Europe, with cars of a
different construction from those used here. There is
reason for believing, however, that the resistance of
American cars is less than that of European cars, and
we have assumed it to be 6 lbs. per ton on a level at
very slow speed, which is less than the resistance which
is usually given, but the following figures should be
regarded merely as an approximation to the actual
facts, of which we are still in ignorance:
Velocity of trains in miles per hour
5
10
15
20
25
30
35
40
45
50
60
70
Resistance on straight line in lbs. per ton (of 2,000 lbs.)
6.1
6.6
7.3
8.3
9.6
11.2
13.1
15.3
17.8
20.6
27
34.6
Now, if we want to get the resistance at 30 miles
an hour of a train of ten cars weighing each 20 tons,
the calculation would be 10 × 20 × 11¹⁄₄ = 2,250 lbs.
This will give the resistance on a level and straight
track. On an ascending grade the resistance is
greater than that given above, because, besides pulling
the car horizontally, it is necessary to raise it vertically
a distance equal to the ascent of the grade. Thus
if we have a grade with a rise of forty feet in a mile, the
amount of energy required to simply raise the weight of
a car would be equal to its weight in pounds multiplied
by the vertical height of the ascent. Thus, supposing
a car which weighs 40,000 lbs. to be run one mile on a
grade of forty feet ascent in that distance, then the
energy expended in simply raising the car will be equal
to 40,000 × 40 = 1,600,000 foot-pounds. Now, if it
was necessary to raise that weight by a direct vertical
lift or pull, it would require a force equal to or a little
greater than the load to do it. But in pulling a car or
train up a grade, which is an inclined plane, the force,
which is the locomotive, instead of being exerted
through the vertical distance is exerted through the
horizontal distance, which in this case is one mile, or
5,280 feet. Therefore, if we divide the number of foot-pounds
of energy required by the distance through
which the power is exerted, it will give us the force exerted
through one foot. That is,
1,600,0005,280 = 151.5 lbs.
The resistance due to the ascent alone of a train on
a grade or incline can therefore be calculated by MULTIPLYING
THE WEIGHT OF THE TRAIN IN POUNDS
BY THE ASCENT IN ANY GIVEN DISTANCE IN FEET
AND DIVIDING THE PRODUCT BY THE HORIZONTAL
DISTANCE IN FEET. Thus in the above example
the rate of the ascent is given in so many feet per
mile; we therefore multiply by 40 and divide by 5,280,
which is the number of feet in a mile. If the rate of
the gradient had been given, as it sometimes is, as 1
in 132, we would simply have divided the weight of
the train by the latter number. If we want to get the
resistance per ton of train we substitute for its weight
that of one ton in pounds; thus:
2,000 × 405,280 = 15.1 lbs.
If, now, we have the resistance which is due to the
ascent or gravity alone, we must add to this the resistance
on a straight and level track, at the speed at
which the train runs, in order to determine the total
resistance on the grade. On a level road at a speed of
5 miles per hour it would be 6.1 lbs. per ton, so that
on a grade of forty feet to a mile at that speed the resistance
would be 6.1 + 15.1 = 21.2 lbs., per ton, and
at 10 miles it would be 6.6 + 15.1 = 21.7 lbs., and
at 30 miles per hour on the grade the resistance would
be 11.2 + 15.1 = 26.3 lbs. per ton. To get the total
resistance on a grade for any speed, we ADD THE RESISTANCE
FOR THAT SPEED ON A STRAIGHT AND
LEVEL LINE TO THE RESISTANCE DUE TO THE ASCENT
ALONE. The resistances for various rates of speed and
grades has been calculated, and is given in the table
in the appendix.
The top horizontal row of figures of that table gives
the rates of speed. The left-hand vertical row gives
the rise of grade in feet per mile. The resistance for
any given grade and speed is given where the vertical
row of figures under the rate of speed and the horizontal
row opposite the rise of the grade intersect
each other. Thus, for a grade of 30 feet per mile and
a speed of 45 miles per hour, we follow the vertical
column under the 45 downward, and the horizontal
column opposite 30 to the right, and where the two
intersect the resistance, 29.1 lbs. is given.
Question 409.What effect do curves have on the resistance
of trains?
Answer. They increase the resistance, but in what
proportion or to what degree is not known accurately.
European authorities say that the resistance is increased,
over what it would be in a straight and level
line, about 1 per cent. for every degree of the curve
occupied by a train. It is probable, however, that the
resistance of American cars, which nearly all have
double trucks, is not so great on curves as that of
European cars, which nearly all have long and rigid
wheel-bases, and whose wheels therefore can not adjust
themselves so easily to the curvature of the track as
they can when the American system of double trucks
is used.
Question 410.What is meant by a degree of a curve?
Answer. In order to measure circles, they are all
supposed to be divided into 360 equal parts, which are
called degrees. One degree of a curve is therefore
¹⁄₃₆₀ of a complete circle; but if the curve has a
long radius, one degree of such a curved track will
be longer than one degree of a curve with a short
radius, but each will have the same amount of
“bend” or curvature. It is this latter which increases
the resistance of trains, and the greater the number of
degrees of a curve occupied by a train of cars, the
greater will be the “bend” of the track, and therefore
the greater the resistance.
Question 411.What other causes affect the resistance
of trains?
Answer. The condition of the track and the force
and direction of the wind. On a rough track the resistance
is very much greater than on a smooth one,
and a strong head-wind makes it much more difficult
to pull a train than it is in calm weather.
PART XXI. PROPORTIONS OF LOCOMOTIVES.
Question 412.In proportioning a locomotive to any
given kind of work, what are the first facts which should
be known?
Answer. We should first know the weight of the
train which the locomotive must draw; second, the
speed at which it must run; and third, the steepest
grades and the shortest curves of the road on which
it must work. From these data the resistance of the
train which the locomotive must overcome can be at
least approximately determined.
Question 413.When the greatest resistance of the
train is known, what is the next thing to be determined?
Answer. As was stated in answer to Question 66, if
the wheels revolve and their adhesion is greater than
the resistance opposed to the movement of the locomotive,
the latter will overcome the resistance; but if the
latter is greater than the friction, the wheels will slip.
It therefore follows that the adhesion must be somewhat
greater than the resistance. As the adhesion is
equal to about one-fifth[100] of the adhesive weight or
pressure of the driving-wheels on the rails, obviously
this weight should be five times the resistance. Thus,
if we have a train weighing 400 tons which we want
to take up a grade of 40 feet per mile at a speed of 20
miles per hour, its resistance, calculated from the table
given in the previous part, would be 9,360 lbs. Therefore,
9,360 × 5 = 46,800 lbs. = the required adhesive
weight.
Question 414.What considerations determine the
manner of distributing this weight on the wheels?
Answer. It is found by experience that if too much
weight is placed upon one wheel, the material of which
the rails are made is partly crushed and injured, and
they then wear out much more rapidly than they
would if the weight was distributed on more wheels,
and thus a smaller amount of weight rested on each
point of contact with the rails. The amount of weight
which can be carried on a single wheel depends upon
the material of which the rails are made, and to some
extent on their form and size, or as the latter is usually
expressed, on their weight per yard.
Question 415.When the adhesive weight and the number
of driving-wheels are known, how is the size of the latter
and of the cylinders determined?
Answer. The size of the wheels will to a certain extent
depend upon the speed, because the larger the
wheels, the further will the locomotive move in one
revolution; but no exact rule can be given for their
size. At present there is still a great diversity of
opinion among engineers regarding the best sizes of
wheels and cylinders for any given service. Probably
the safest plan will be to consult the best practice, and
in the absence of any better reasons be guided for the
present by that. In this country the most common
size of locomotives used is that which we have selected
for our illustrations, that is, what are called five-feet
wheels, and cylinders of 16 inches diameter and 24
inches stroke. More engines of these dimensions are
used than of any other. For freight service the wheels
are sometimes made of smaller and for passenger trains
of larger diameter; but locomotives with driving-wheels
and cylinders of the dimensions given are used
for both passenger and freight service. It should be
stated here that what are called five-feet wheels are
usually about 1¹⁄₂ in. larger in diameter than five feet.
This arose from the fact that the tires which are now
used are made thicker than they were on the first engines,
and the practice thus established has been continued.
We will therefore take the diameter of what
is called a five-feet wheel at what it really is, 61¹⁄₂ in.
Such locomotives also have about 40,000 lbs. of adhesive
weight. Now, the circumference of such wheels
is 193.2 in., and therefore in one revolution of the
wheels, if they do not slip, the locomotive will move
that distance on the rails. At the same time each
piston will sweep through the cylinder twice, and
therefore in one revolution 4 times one cylinder full of
steam is used. Now a cylinder of 16 in. diameter and
24 in. stroke contains or will hold 4,825¹⁄₂ cubic inches,
so that in one revolution of the wheels 4,825¹⁄₂ × 4 =
19,302 cubic inches of steam are used. As has been
stated, in one revolution of the wheels, if they do not
slip, the locomotive will move 193.2 in. If, now, we
divide 19,302 by 193.2 it will give us the amount of
steam used to move the locomotive and train one inch.
Now, 19,302 ÷ 193.2 = 99.9, which, for the sake of even
figures we will call 100. We thus see that a locomotive
with 40,000 pounds or 20 tons (of 2,000 lbs.) of
adhesive weight requires 100 cubic inches of cylinder
capacity[101] to move it one inch. Now, if a locomotive
had only half as much weight on the driving-wheels,
it could pull only half as much load, and would therefore
use only half as much steam, and consequently
need only half the cylinder capacity of the other locomotive.
If there was three-quarters or a third as
much adhesive weight, the cylinder capacity should also
be three-quarters or a third. We thus see that the
cylinder capacity should be proportioned to the total
adhesive weight. Now as 100 cubic inches of cylinder
capacity are needed to move an engine with 20 tons
adhesive weight one inch, if we divide 100 by 20 we
will get the cylinder capacity needed for each ton.
That is, 100 ÷ 20 = 5 CUBIC IN. CYLINDER CAPACITY
PER TON (of 2,000 lbs.) OF ADHESIVE WEIGHT IS
NEEDED TO MOVE ANY LOCOMOTIVE ONE INCH. This
quantity we have named the modulus of propulsion.
[101] The cylinder capacity is the space swept through by the two pistons.
In the above illustrations what is meant is, that the average space in the
cylinder swept through by the piston is 100 cubic inches for each inch
that the locomotive advances.
Supposing now that it is required to calculate the
cylinder capacity for a locomotive with 15 tons adhesive
weight, and wheels 4¹⁄₂ feet or 54 in. in diameter.
We will first multiply 15 by the modulus of propulsion,
15 × 5 = 75 = the number of cubic inches of cylinder
capacity required to move such a locomotive one
inch. Multiplying the length of the circumference of
the wheels, which in this case is 169.6 in. by 75, will
give us the total cylinder capacity for one revolution.
That is 169.6 × 75 = 12,720 cubic inches of cylinder
capacity, or the space which should be swept through
by the two pistons. Dividing this by 4 will give us
the cubical contents in inches of one of the cylinders.
Thus, 12,720 ÷ 4 = 3,180 cubic inches = the capacity
of one cylinder. Now as the capacity of a cylinder is
calculated by multiplying the area of the piston by
the length of the stroke, if we have the one we can
easily determine the other. Thus, supposing it was
intended to make the stroke of the pistons 22 in., dividing
3,180 by 22 will give us the area of the piston.
Thus, 3,180 ÷ 22 = 144.5 square inches. Now by the
well-known rule in mensuration, if we DIVIDE THE
AREA OF A CIRCLE BY 0.7854, THE SQUARE ROOT OF
THE QUOTIENT WILL BE THE DIAMETER OF THE CIRCLE.
Thus, 144.5 ÷ 0.7854 = 183.9. The square root
of 183.9 is 13¹⁄₂ nearly, which should be the diameter
of the cylinder. Instead of calculating the diameter
of the circle, a more convenient way is to refer the
area to a table of areas, and from it find the diameter.
Of course if we have the diameter of the piston and
want to get the stroke, we DIVIDE THE CUBICAL CONTENTS
OF THE CYLINDER BY THE AREA OF THE PISTON.
Thus, in the present illustration, if it was intended
to have the piston 13¹⁄₂ in. diameter, we would
have divided 3,180 by the area of a piston 13¹⁄₂ in.
diameter, which is 143.1, so that we would have 3,180
÷ 143.1 = 22 nearly, = inches of stroke of piston.
From the above considerations we can deduce the
following RULE FOR CALCULATING THE CAPACITY
OF THE CYLINDERS WHEN THE ADHESIVE WEIGHT IS
KNOWN:
Multiply the total weight on the driving-wheels
in tons (of 2,000 lbs.) by 5, and then by
the circumference of the wheels in inches,
and divide by 4. the quotient will be the
cubical contents in inches of each cylinder.
From this, if either the diameter or stroke is given the
other can easily be found, as has been explained.
It should be remarked here that it is unimportant,
so far as the power of the locomotive is concerned,
whether the cylinders have a large diameter and a
short stroke or a small diameter and a long stroke,
provided the cubical contents are the same. Thus
cylinders 17¹⁄₂ in. in diameter and with 20 in. stroke
would have almost exactly the same capacity and the
same power would be exerted with them as with cylinders
16 × 24 in.; the only difference would be that
with the cylinder of the largest diameter the pressure
on the piston and consequently on the crank-pin journal
and the strain on the parts would be greater than
with the smaller cylinder. The difference in pressure
would, however, be exactly compensated by the loss or
gain in the leverage exerted through the driving-wheels
on the rails.
Question 416.What circumstances should determine
the size of locomotive boilers?
Answer. They should be proportioned to the amount
of adhesive weight, and to the speed at which the locomotive
is intended to work. Thus, a locomotive with
a great deal of weight on the driving-wheels could
pull a heavier load and would, by the above rule for
proportioning the cylinders, have a greater cylinder
capacity than one with little adhesive weight, and
would therefore consume more steam, and therefore
should have a larger boiler. It is also obvious that if
a locomotive like that shown in plates I and II should
have a boiler just large enough to furnish steam when
running at the rate of 20 miles an hour, it would be
too small if the locomotive ran 40 miles an hour, the
train resistance being the same in both cases. Driving-wheels
5 feet in diameter would at 20 miles per hour
make 112 revolutions per minute, and would therefore
consume 448 cylinders full of steam. At 40 miles per
hour double the number of revolutions would be made,
and consequently twice the quantity of steam would
be used, and therefore the boiler should have twice the
steam-producing capacity. If, therefore, we know the
size of a boiler required for a given amount of adhesive
weight and a given speed, we can easily calculate
the boiler capacity for any other weight and speed.
Question 417.How can we determine the boiler capacity
needed for an engine with a given amount of adhesive
weight and for a given speed?
Answer. This must be determined empirically, that
is from experience.
Question 418.On what does the steam-generating
capacity of a boiler depend?
Answer. First, upon the size of its grate and fire-box,
because more fuel can be burned in a large fire-place
than in a small one; second, on the amount of
heating surface to which the products of combustion
are exposed, and third, on the draft produced by the
blast or exhaust steam. Of course the amount of
steam generated is also dependent upon a great variety
of other circumstances, such as the nature of the
combustion, the firing, the arrangement of the fire-box,
grates, etc., and the condition of the heating surfaces;
but these have nothing to do with the proportions
or size of the boiler.
Question 419.What are the proportions of boilers
used in locomotives like that which has been illustrated in
these articles and represented in Plates I and II?
Answer. The area of the grate is about 2,100 square
inches and the total heating surface about 800 square
feet, and the water capacity about 5,000 lbs., and the
total weight of the boiler, including all the boiler attachments
and appliances for promoting combustion,
about 30,000 lbs.
Question 420.At what speed are such engines usually
run?
Answer. The speed varies so much under different
circumstances, that it is impossible to give even approximately
the average speed of such engines.
Question 421.How then can we determine the proper
proportions of a boiler for a locomotive intended for any
given service?
Answer. As stated before, this can only be done empirically.
The safest method is to select a locomotive
which is doing the best service, and learn the average
speed at which it runs, the size of its grate and the
amount of its heating surface, and its adhesive weight.
Now multiply the above speed in miles per
hour by the adhesive weight of the locomotive
in tons (of 2,000 lbs.) and divide the product
into the area of the grate in square inches.
Then multiply the adhesive weight of the
locomotive for which the boiler is to be
provided by its speed, in miles per hour, and
by the quotient obtained above: the product
will be the area of the grate in square inches
for the new engine. To illustrate this, suppose
an engine of the dimensions given to run at an average
speed of 20 miles per hour. Now, multiplying
that speed by the number of tons of adhesive weight
and dividing the product into the area of the grate, we
have 20 × 20 = 400 and 2100 ÷ 400 = 5.25. We now
want to determine the size of a grate for the boiler of
a locomotive with 30 tons adhesive weight and to run at
a speed of 15 miles per hour. We therefore multiply
15 by 30 and the product by the above quotient, or
15 × 30 × 5.25 = 2,362.5 = square inches of grate surface
for the boiler. The required heating surface can
be obtained in a similar way, by substituting it instead
of the grate surface in the calculations.
Question 422.How is the size of locomotive boilers
usually limited?
Answer. By the weight of the locomotive and to
some extent by the distance between the rails. It will
be found often that it is impossible to make the boiler of
the size indicated by a calculation similar to the above
without at the same time making the weight of the
locomotive and the adhesive weight greater than was
assumed. The result of such a calculation indicates,
therefore, that too large a proportion of the weight of
the locomotive is on the driving-wheels for the speed
at which it is intended to work, and that either they
should bear less weight or the speed be reduced.
Question 423.In what respects is the operation of
locomotive boilers different from that of nearly all other
steam boilers?
Answer. The amount of steam generated in proportion
to the amount of heating surface is much greater
in locomotive boilers than in any other kind. To
produce combustion which will be sufficiently active
to generate the requisite quantity of steam, the fire
must be stimulated by the blast created by the exhaust
steam to a degree unknown in other kinds of boilers.
So rapid is the movement of the products of combustion
that a smaller proportion of the heat is imparted
to the water contained in the boiler, and consequently
a less amount of water is evaporated in proportion to
any given amount of fuel than in boilers in which
combustion is less violent. The combustion is also
less perfect, because the strong draft does not allow
time for a perfect combination of the gases which produce
combustion.
The supply of steam which a locomotive boiler must
furnish is also much more irregular than the demands
made upon any other kind of boiler. At one time the
fire must be urged to the greatest possible intensity
in order to furnish steam enough to pull a train up a
steep grade. When the top is reached the demand
ceases, and the boiler can be cooled. The load which
a locomotive can pull over a given line of road is
usually limited by the utmost capacity of the boiler to
supply steam at these critical periods.
Question 424.What relation is there between this irregular
action and the size of the boiler?
Answer. The smaller the boiler, or rather the larger
the amount of steam which must be generated in a
given time in proportion to the heating surface, the
more must the fire be urged; and therefore the smaller
the boiler in proportion to the work it must do, the less
will be its economy. In order to produce a rapid combustion
in a small boiler, it is necessary to contract
the exhaust nozzles in order to create a draft strong
enough. In doing this the back pressure on the pistons
is very much increased, and when the blast becomes
very violent a great deal of solid coal is carried
through the tubes and escapes at the smoke-stack unconsumed.
At the same time large quantities of unconsumed
gases escape, because there is not time for
combustion to take place in the fire-box. The fact
that with a violent draft the flame and smoke are in
contact with the heating surface for a sensibly shorter
period of time also has its influence; as less heat will
be imparted to the water if the products of combustion
are only ¹⁄₁₀₀ of a second instead of ²⁄₁₀₀ in passing
through the tubes.
There is another consideration which should be
taken into account in this connection, which is, that if
a boiler is so small that it is worked nearly up to its
maximum capacity at all times, it will be impossible
to accumulate any reserve power in it in the form of
water heated to a high temperature to be used as occasion
may require. With a boiler having a great
amount of heating surface and capacity for carrying a
large quantity of water, the latter can be heated at
times when the engine is not working hard, and the
heat thus stored up in the water can then be used when
it is most needed. Thus we will suppose that to pull a
train of cars on a level 250 lbs. of steam are consumed
per mile. On a grade of 30 feet per mile the resistance
will be three times what it is on a level, and
therefore three times the quantity of steam will be
consumed, so that the boiler must then evaporate 750
lbs. of water per mile. Now to convert 250 lbs. of
water heated up to a temperature due to 130 lbs. of
effective pressure, or 355.6 degrees, into steam of that
pressure will require 216,575 units of heat. If at the
same time that this steam is being consumed, we pump
into the boiler 250 lbs. of water of a temperature of
60 degrees, 73,900 more units of heat will be needed
to raise the water to the temperature due to 130 lbs.
effective pressure, so that on the level part of the road
it would be necessary to transmit to the water in the
boiler 216,575 + 73,900 = 290,475 units of heat in a
mile. If there is no room in the boiler for storing a
surplus quantity of hot water, it will be necessary on
a grade as fast as the steam is consumed to feed an
equivalent amount of cold water to take the place of
that which was converted into steam, so that on a 30
feet grade it would be necessary to convert at the rate
of 750 lbs. of hot water into steam in a mile, which
would require 649,725 units of heat, and at the same
time heat an equal amount of cold water to a temperature
due to the pressure of the steam, which would
require 221,700 more units. So that it will be necessary
to transmit at the rate of 871,425 units of heat
to the water per mile. Now if the boiler was so large
that more water could be pumped into it and heated
than was used on the level portion of the road, and
could there be stored up for future use, the pumps
might be either partly or entirely shut off when the
engine was working the hardest on the grade. In this
way, instead of being obliged to convert hot water
into steam, and at the same time heat an equal amount
of cold feed-water, there would be a surplus of hot
water stored up already heated. It would therefore
only be necessary to convert this hot water into steam,
which will require a transmission of heat to the water
at the rate of 649,725 units of heat instead of 871,425.
It must be remembered that on nearly all roads there
are certain difficult places which practically limit the
capacity of the locomotives on that line. If therefore
the capacity of the engines can be increased at those
points, their capacity over the whole line is increased.
It will be seen by the above illustration that by having
a large boiler it is necessary for it to do very much
less work at the critical period, when, as every locomotive
runner knows, it is often of the utmost importance
to make use of every possible available means in
order to pull the trains. It is true that on a very
long grade the supply of surplus hot water would soon
be exhausted, but even in such cases there is usually
one place, owing to a curve or other cause, which is
more difficult to surmount than any other, in which
case it will be necessary to use more steam for a short
time than the locomotive can generate if the boiler is
fed continuously. For such cases a surplus of water
can be used. But even if the resistance is equal over
the whole length of the incline, still the large boiler
will have the advantage, because it can at all times
generate more steam than a smaller one. It may
therefore, we think, safely be assumed that locomotive
boilers should always be made as large as the weight
of the locomotive will permit.
Question 425.What effect does the size of the driving-wheels
have upon the combustion and evaporation of locomotive
boilers?
Answer. As small wheels make more revolutions in
running a given distance than large ones, there will
be more strokes of the piston with the former than
with the latter, if the locomotive in both cases runs at
the same speed. As smaller cylinders are usually employed
with small wheels, the blast up the chimney is
then composed of a larger number of discharges of
steam, but each one of less quantity, than when larger
wheels and cylinders are used. In the one case the
“puffs” of steam are many and small, and in the latter
few and large. If the cylinders are proportioned
by the rule which has been given for that purpose, the
amount of steam discharged in running any given distance
will be the same with engines having large
and those with small wheels, the only difference being
that it will be subdivided into a greater number of
discharges in the one case than in the other. Now, it is
found that the draft of engines is much more effective
on the fire when the blast is thus subdivided, that is
when small wheels and cylinders are used, than it is
with large ones, and therefore more steam is generated
with the former than with the latter.
Question 426.What relation is there between the size
of the wheels and that of the boiler?
Answer. As has been explained, the size of the
boiler is limited by the weight of the locomotive. The
boiler and its attachments of an American locomotive,
when the former is filled with water, weigh about half
as much as the locomotive; therefore unless we increase
the weight of the latter or decrease the weight
of the machinery, we can not increase the size of the
boiler. Now, large wheels are heavier than small
ones; they require larger cylinders, stronger connections,
heavier frames, and in fact nearly all the parts
of the machinery used with large wheels must be
heavier than are required when small wheels are used.
Therefore, by decreasing the size of the wheels all the
other parts of the engine proper can be made lighter
than is possible if large wheels are used, and thus the
size and weight of the boiler can be increased without
increasing the whole weight of the locomotive.
There is of course a practical limit below which the size
of the wheels can not be reduced, because the speed of
the piston would become so great as to be injurious to
the machinery. By reducing the stroke, however, with
the diameter of the wheels, the evil referred to may be
obviated to a great extent. A cylinder with a large
diameter and comparatively small stroke has also the
advantage that there is less surface exposed to radiation
of heat than there is in a cylinder in which these
proportions are reversed.
PART XXII. DIFFERENT KINDS OF LOCOMOTIVES.
Question 427.Into what classes may locomotives be
divided conveniently?
Answer. 1. Locomotives for “switching,” “shunting”
or “drilling” service, that is, for transferring
cars from one place to another at stations; 2, for
freight traffic; 3, for ordinary passenger traffic, and 4,
for suburban or metropolitan railroads, where a great
many light trains are run.
Question 428.What kinds of locomotives are used in
this country for switching cars at stations?
Fig. 220.
Answer. Four-wheeled locomotives similar to that
shown in Plate IV. In some cases they are made
with six driving-wheels. Engines like that shown in
Plate IV have separate tenders, but they are sometimes
made so as to carry the water-tank and fuel on
the locomotive itself, as shown in fig. 220, and are
then called tank locomotives. Fig. 220 represents a
switching engine built by the Taunton Locomotive
Manufacturing Company.
Question 429.Why are four-wheeled locomotives used
for switching?
Answer. Because in such service it is constantly
necessary to start trains, many of which are very
heavy, and therefore a great deal of adhesion is needed.
For this reason the whole weight of the locomotive
and in the case of tank locomotives that of the water
and fuel is placed on the driving-wheels. It is also
necessary for such locomotives to run over curves of
very short radius and into switches whose angle with
the main track is very great, and therefore in order
that they may do this and remain on the track, their
wheel-bases must be very short, and consequently the
wheels are all placed near together between the smoke-box
and fire-box.
Question 430.Why are such locomotives not suited
for general traffic?
Answer. Owing to the shortness of their wheel-bases
they become very unsteady at high speeds, and acquire
a pitching motion, similar to that of a horse-car
when running rapidly over a rough track. This unsteadiness
not only becomes very uncomfortable to the
men who run the locomotive, but there is danger of
the engine running off the track. As nearly all
switching is done at very slow speeds, it is not so objectionable
for that service as it would be on the “open
road”[102] at high speeds.
[102] The term “open road” is a literal translation from the German, for
which there is no corresponding English term, and means the road between
stations where trains run fast.
Question 431.What kinds of locomotives are used
for freight service?
Answer. The greater part of the freight service of
this country is performed by locomotives like that selected
for the illustrations of these articles, and represented
in Plates I, II and III. Such locomotives have
been called “American” locomotives because they first
originated in this country and are now more generally
used here than anywhere else. Side elevations of locomotives
of this kind, built by the Baldwin Locomotive
Works, the Grant Locomotive Works, the Danforth
Locomotive and Machine Company, the Mason
Machine Works and the Hinkley Locomotive Works
are represented in Plates V, VI,
VII, VIII and IX.
Such locomotives have been described in the preceding
pages.
Question 432.What are the dimensions of such engines?
Answer. The principal dimensions of the engines
illustrated are given in the table in the appendix, but
locomotives of this plan are built of much smaller and
also of larger sizes than those represented by the engravings.
In some cases such locomotives do not
weigh more than 35 or 36,000 lbs., with cylinders
from 8 to 12 inches in diameter. In other cases they
weigh as much as 66,000 lbs., with cylinders 17 or 18
inches in diameter. The wheels vary from 4 to 6 feet
in diameter, but the most common sizes are 4¹⁄₂ and 5
feet.
Question 433.When it is desirable to pull heavier
loads than is possible with the adhesive weight that can be
placed on four driving-wheels, what is done?
Answer. One or more pairs of driving-wheels are
added, as in the ten-wheeled locomotive represented
in Plate X, the “Mogul” engine, Plate XI, and the
“Consolidation” engine, Plate XII. The ten-wheeled
locomotive, it will be seen, is similar in construction to
an ordinary American locomotive, excepting that it
has another pair of driving-wheels in front of the
main driving-wheels. It will be seen, however, that
it is necessary to keep these close to the latter, because
if they are brought further forward they will be
too near the back truck-wheels. For this reason a
truck consisting of a single pair of wheels, A, A, is
placed in front of the cylinders, as represented in
Plates XI and XII, is now much used. The front
driving-wheels are then placed further forward, and
thus bear a larger proportion of weight than they do
in locomotives like that shown in Plate X.
Question 434.How are trucks with a single pair of
wheels constructed?
Answer. The truck frame is extended some distance
behind the truck-axle, as shown in fig. 221, and the
centre-pin, a, about which it vibrates, is placed at the
back end. The weight of the locomotive, or that portion
to be carried on the truck, is then made to rest
over the centre of the axle, but in such a way that it
can move laterally or crosswise over the track. Such
trucks were first made so that the weight of the engine
rested on slides on the truck frame, but recently
they are nearly always suspended on links, so that they
can swing like a pendulum, as shown in figs. 190 and
191. The weight of the engine then rests on the centre-plate,
H H; which forms part of the plate, B B.
This is suspended by links, L L, represented by dotted
lines, which are attached by bolts to the cross-pieces,
m m, which are fastened to the truck frame. In this
way the truck-wheels can move sideways independent
of the engine itself. As the wheels and axles, A A,
must move about the centre-pin, a, fig. 221, the axle
assumes a radial position to the curves of the track.
It does this, too, quite independent of the driving-wheels,
as is shown in fig. 221, which represents a
plan of the wheels on a curve. It will be seen that
the truck is not at all influenced by the position of the
driving-wheels. This arrangement therefore gives
great flexibility to the wheel-base, and enables the
wheels to adjust themselves to any lateral curvature
or alignment of the track.
Fig. 221. Scale ¹⁄₈ in. = 1 foot.
Question 435.For what purpose are locomotives like
that shown in Plates XI and XII used?
Answer. “Mogul” locomotives are often used for ordinary
freight service where heavy trains must be hauled,
and also on steep grades. “Consolidation” locomotives,
represented in Plate XII, which have eight driving-wheels,
are employed almost exclusively for traffic over
heavy mountain grades.
Question 436.What other kinds of locomotives are
used for freight traffic?
Answer. Various kinds of tank locomotives, that is,
locomotives which have no separate tenders, but carry
the water-tanks and fuel on the frame and wheels of
the locomotive itself, have been devised and are to
some extent used. Plate XIII represents a locomotive
of this kind on which the tanks are placed on
each side of the boiler, and the fuel on a Bissell truck
at the back end. A similar truck is placed at the
front end, so that a locomotive of this kind can run
equally well either way. The lateral movement of
the two trucks also gives great flexibility to the wheel-base,
so that such an engine will adjust itself easily to
the curvature of the track. If, however, the two pairs
of truck-wheels should both stand on an elevated part of
the track, and the driving-wheels on a depression, the
latter would evidently not carry as much and the
truck-wheels would carry more of the weight of the
engine than they did on a level part of the track. If
the reverse condition of things should occur, that is, if
the driving-wheels should be on an elevation and one
or both pairs of the truck-wheels on a depression,
then the latter would bear less weight than they did
and the driving-wheels more. For this reason, in
order to distribute the weight evenly on all the wheels,
it is necessary to equalize the weight on the truck
and driving-wheels, by connecting them with equalizing
levers, similar to those which were described in
answer to Question 301. These levers distribute any
undue weight which may come on one wheel to that
next to it. This is important, because if the driving-wheels
bore less weight at some times than at others,
their adhesion and their capacity to draw loads would
be reduced in like proportion.
It is evident, however, that if the water-tank or
fuel is carried on the driving-wheels, there will be a
greater weight on them when the tank is full than
when it is empty, and that therefore there will
either be so much weight on the wheels at one time
as to be injurious to the rails, or else there will be too
little for adhesion at another. Of course cases are
conceivable, and doubtless exist in practice, where
more adhesion is required to start a train and haul it
during the first part of the “run” than will be needed
during the latter part. In such cases doubtless the
variable character of the weight might be an advantage
instead of the reverse, but for ordinary practice
a variable load on the driving-wheels would have the
disadvantages which have been described. For this
reason tank locomotives have been built like that represented
in Plate XIV. In this it will be seen that
the weight of the water-tank rests on a four-wheeled
truck at the back end. A Bissell or two-wheeled
truck is, however, placed in front in the same position
as in the engine represented in Plate XIII, and carries
a portion of the weight of the boiler and machinery.
In order to get all the advantages which a four-wheeled
switching engine possesses in having its
whole weight on the driving-wheels, and at the same
time avoid the disadvantages which result from a short
wheel-base, and also from a varying amount of weight
on the driving-wheels, a locomotive like that represented
in Plate XV was designed by the writer with
the whole weight of the boiler and machinery resting
on the driving-wheels, and the water and fuel on a
truck. By this means not only the objections to carrying
the weight of the water on the driving-wheels is
overcome, but at the same time the disadvantages
arising from the short wheel-base of the switching locomotive,
Plate IV, are also obviated. That is, all the
permanent weight of the boiler and machinery of such
a locomotive rests on the driving-wheels, and is therefore
all adhesive weight, as it is in the switching engine,
and at the same time by extending the frame
beyond the fire-box and placing the water-tank and
fuel on this extension of the frame and supporting
their weight on a truck, the engine has a wheel-base
which is as long and as flexible as that of ordinary
American engines, represented in Plates V, VI, VII,
VIII and IX, and as the latter have only about two-thirds
of their weight on the driving-wheels, locomotives
like that represented in Plate XV, of the same
weight as the others, have fifty per cent. more adhesion,
or they may be one-third lighter and have the
same adhesion. As was explained in answer to Question
260, if an ordinary American locomotive runs
backwards, that is, with the driving-wheels in front,
the friction of their flanges against the rails on curves
of short radius will be very excessive. To avoid this
with locomotives of the design last described, they are
run with the truck first, which, being at the opposite
end of the boiler from the position which it usually occupies,
reverses the position of the boiler and other
parts relative to the motion of the engine. That is,
the fire-box is then in front and the smoke-stack behind.
Engines of this kind have been built and are
now working and doing excellent service; but the
prejudice which exists against running locomotives in
the reverse direction to what has been customary
seems to be the chief obstacle in the way of their use.
Another plan which possesses all the advantages of
the locomotive described above and is free from the
last objection is represented in Plate XVI. This
plan was first adopted by Mr. Robert Fairlie in England,
but has been introduced into this country and
very much improved by Mr. William Mason, of Taunton,
Mass. In these locomotives, the driving-wheels
and cylinders are attached to a truck frame which
turns around a centre-pin like any ordinary truck.
The steam and exhaust pipes are connected to the
boiler and cylinder with pipes which have flexible
joints. By this means the truck can move independently
of the boiler, and thus the driving-wheels can
adjust themselves to the curvature of the track, just as
the wheels of any other truck do, and therefore the
driving-wheels can be run ahead just as well as the
truck-wheels which carry the tank. This plan possesses
the additional advantage that the fire-box can
be made as wide and as long as may be desired without
interfering with the driving-wheels. The flexible
pipes are, however, usually considered an objection;
but with the improvements which have been made in
their design and construction, the difficulties which
were at first encountered have probably been overcome.
At any rate if there is no other objection to
the use of such locomotives, ingenuity and care should
in time overcome that one. Plate XVII represents a
locomotive of this plan, with six driving-wheels and a
six-wheeled carrying truck under the tank. This latter
plan of locomotive is intended for heavy freight
traffic.
Question 437.What kind of locomotives is used for
passenger trains?
Answer. Eight-wheeled American locomotives are
used almost exclusively for passenger service. Usually
the driving-wheels of such locomotives are larger
in diameter than are used for freight traffic. Their
size varies from 5 feet to 5 ft. 9 in. in diameter. The
locomotive by the Mason Machine Works represented
in Plate VIII has 5¹⁄₂ feet driving-wheels. For very
heavy express trains locomotives with 17 × 24 inch
cylinders and weighing 34 tons are now used on many
through lines.
Question 438.What is meant by suburban and metropolitan
railroads, what is the nature of their traffic,
and what kinds of locomotives are needed for it?
Answer. The traffic of suburban railroads consists
chiefly of the transportation of passengers who do
business in the city to the latter in the morning and
to their homes in the evening. As the largest number
of passengers must be carried during a few hours
in the morning and evening, it is necessary to run
very heavy trains at those times. As the passengers
must be distributed at many stations which are near
together, it is necessary to stop often; and in order
that the average speed may be reasonably fast the
trains must run very rapidly between these stations.
It is therefore necessary to have heavy locomotives,
with more than the usual proportion of adhesive
weight, so that the trains can be started quickly without
slipping the wheels. The main valves should also
have a liberal amount of travel, so that steam will be
admitted to and exhausted from the cylinders quickly.
In some cases it is thought desirable to have locomotives
which will run equally well either way, so that
it will not be necessary to turn them around at each
end of the “run.”
By metropolitan railroads are meant railroads in
large cities. They may be divided into two classes,
one for carrying freight cars from the outskirts of
cities to the warehouses and stores at their business
centres, and also from the terminus of one road to that
of another. Metropolitan railroads of this kind are
usually branches of lines which extend from the city.
Locomotives for such traffic must have great tractive
power, in order to pull heavy trains, and as the speed
is usually slow the wheels and the boiler capacity may
be small. They must generally be capable of running
through curves of very short radius; and as the traffic
is usually carried through streets in close proximity to
buildings, the locomotives should be as nearly as possible
noiseless. The other class of metropolitan roads
is for carrying passengers. The traffic of the latter is
similar to that usually carried on horse railroads, and
consists almost exclusively of passengers. At present
(1874) there are only one or two metropolitan railroads
in this country for carrying passengers which
are operated by steam power. It seems certain, however,
that their use will soon become very general in
all large cities. Their traffic will consist of many
light trains run at short intervals and at comparatively
slow speeds, and therefore very light locomotives
are required.
Question 439.What kinds of locomotives are used
for suburban railroads?
Answer. The ordinary American eight-wheeled locomotive
is used more than any other kind; but a number
of locomotives like that represented by fig. 222
have been built and are used for this traffic. These
have one pair of driving-wheels in front of the
main pair and a Bissell truck in front of the cylinder.
With this arrangement the driving-wheels bear
a larger proportion of weight than they do if arranged
on the ordinary American plan with a four-wheeled
truck. Another plan is that shown in Plate XVIII.
Such engines, as will be seen, have a Bissell truck at
each end, and therefore they run equally well either
way. In some cases the tanks of such engines are
carried on the top and sides of the boiler. When
they are obliged to run only a short distance, and a
small supply of water is needed, this arrangement answers
very well; but it is impossible to carry a large
supply of water in this way without overloading the
wheels of the locomotive, and at the same time increasing
the evils of a varying load on the driving-wheels.
Fig. 222. Light Passenger and Freight Locomotive,
By the Grant Locomotive Works, Paterson, N. J.
Locomotives like that shown in Plate XIV are also
used for suburban traffic. As shown in the engraving
they have a four-wheeled truck at one end and one
with two wheels at the other, so that it is thought
that they can be run safely either way. The four-wheeled
truck carries the weight of the water and
fuel.
The plan of engine represented by Plate XV is very
well adapted for this kind of traffic. Excepting on
curves with a very short radius it could be run in
either direction at any required speed, without encountering
any other difficulty excepting the prejudices of
those who run it.
As double-truck locomotives similar to that shown
in Plate XVI can adjust themselves to any curve, this
objection could not be urged against their use.
Question 440.What kinds of locomotives are used on
metropolitan railroads?
Answer. For freight traffic ordinary switching locomotives
like that represented in Plate IV are often
employed. In some cases these have the tanks on the
locomotives. It often happens, though, that such
traffic must be conducted in the streets of a city, and
that the noise, especially of the exhausting steam, is
thus liable to frighten horses and disturb the occupants.
It is, then, necessary either to condense the
exhaust steam or render its escape noiseless, which is
done by allowing it to escape into the water-tanks.
Street locomotives which have a condenser similar to
the surface condensers used on marine engines are
used on the Hudson River Railroad in New York.
The exhaust steam passes through these and then escapes
into the tanks. The latter are long and narrow,
so as to expose a great deal of surface to radiation,
and in this way cool the water which becomes
heated by the steam. The engines have four driving-wheels
and vertical boilers. The cylinders are connected
to a crank shaft with a pinion on it, which
gears with another wheel of larger size on the driving-axle.
In this way the speed is reduced and great
tractive power can be exerted. The whole of the engine
is enclosed so as to hide the machinery, the sight
of which is supposed to frighten horses. The engines
were designed and patented by Mr. A. F. Smith, formerly
Master Mechanic of that road.
For roads in cities carrying passengers almost exclusively,
an entirely different class of locomotives is
needed. To suit passengers it is of course necessary
to run a great many trains at very short intervals.
When this is done the trains are necessarily very light,
and therefore only light locomotives are needed. Plate
XIX represents the locomotives employed on the
Greenwich Street Elevated Railroad in New York.
These engines weigh only 10,000 lbs., and the wheels
are 30 in. diameter and the cylinders 7 × 10 in. The
peculiarity in their construction consists in their having
an intermediate shaft between the two pairs of driving-wheels.
This shaft has two cranks inside of the
frames and two outside. The cylinders are connected
to the inside cranks, and the coupling-rods to those on
the outside. The water is carried in a tank on top of
the boiler. The fuel is anthracite coal.
PART XXIII. CONTINUOUS TRAIN BRAKES.
Question 441.What are meant by automatic or continuous
train brakes?
Answer. Continuous train brakes are brakes which
can be applied to all the cars of a train by the locomotive
runner on the locomotive. In some cases such
brakes are arranged in such a way that they can also
be applied from any car in the train, or are made self-acting
in case of an accident, such as a car getting off
the track or a train breaking in two.
Question 442.What are the principal systems of
brakes of this kind in use?
Answer. What is called, after its inventor, the Westinghouse
atmospheric brake is now used more than
any other. Next to this, Smith’s vacuum brake is
used most. Besides these two, Creamer’s, Ward’s,
Loughridge’s and Henderson’s systems of brakes are
used to a limited extent. The two first are, however,
the only ones which have come into sufficiently extensive
use as yet to justify us in describing them here.
Question 443.How does the Westinghouse brake act
and how is it constructed?
Answer. As its name indicates, the medium employed
for transmitting the power for operating the
brakes is atmospheric air.
Fig. 223. Scale ¹⁄₂ in. = 1 foot.
This is compressed to any required density by a
steam pump which is located between the driving-wheels,
or in any other convenient place on the locomotive.
This pump is shown in section in fig. 223
and consists of two cylinders, the upper one, A, the
steam cylinder, the piston of which is connected by
its rod with the piston in the lower cylinder, B. This
latter is operated by the steam piston, and at each
stroke a quantity of air, equal to the space swept
through by the lower piston, is compressed and thus
forced into a cylindrical reservoir, which is usually
placed under the foot-board of the locomotive, in which
it is stored for use at any time when the brakes are to
be applied. The air and steam cylinders are supplied
with suitable valves for admitting and releasing the
air and steam. From this reservoir it is conducted
back under the tender and cars by pipes, which are
connected together between the engine and tender and
between the cars by India rubber hose. Two pieces
of hose are attached to the engine and also to each end
of the tender and cars, so that in case one piece should
break the others will act. Each of these pieces is
united or coupled to the corresponding piece opposite
to it by a peculiar coupling made for the purpose, so
that they can be quickly disconnected if the cars, engine
or tender are uncoupled.
Under the tender and also under each car is a cylinder
and piston. The compressed air is conducted to
this cylinder in front of the piston when the brakes
are to be applied. As the piston-rod is connected by
a bell crank to the brake levers when the piston is
forced out by the pressure of the air, the brakes are at
once applied to the wheels. As the reservoir under
the foot-board is connected by the pipes which have
been described with the cylinders under each car and
the tender, by simply opening communication between
the reservoir and the pipes, the air at once rushes from
the reservoir back through the whole length of the
train, and so rapid is its motion and quick its action
that only a second or two intervenes between the
opening of communication and the application of the
brakes. To relieve or “let off” the brakes it is only
necessary to close the reservoir cock and open communication
from the air-pipes to the external atmosphere,
when the compressed air in the brake cylinders will
escape, and the springs ordinarily used on car brakes
will cause the pistons to resume their former positions.
For the purpose of opening the connection from the
reservoir to the brake cylinder, and closing this connection
and opening one from the latter to the external
air, a single three-way cock is commonly used.
This is arranged at such a point as to be under the
control of the engineer, so that he can at pleasure turn
on the compressed air with any degree of force, instantaneously,
or slowly, or with a varying power, or
by another turn of the cock let it off as freely, still
keeping it under the same complete control.
Fig. 224. Scale 1¹⁄₂ inch = 1 foot.
Question 444.How does the vacuum brake act and
how is it constructed?
Answer. The power is applied to the brakes of the
cars in this system by exhausting instead of compressing
the air. This is done by means of an ejector, of
which fig. 224 is a section. This operates somewhat
like an injector. Steam is admitted into the pipe B,
and escapes through the annular or circular opening
a a. The effect of this is to create what is called an
“induced current,” or to draw the air from the pipe
C′ C, which, with the steam, escapes at A. This produces
a partial vacuum in the pipe C, which extends
back under the cars. The pipes under the cars
are connected together by rubber hose, which are prevented
from collapsing by coils of wire inside. Under
the tender and under each car are India rubber cylinders
with cast iron ends, one fastened to the car and
the other movable. The rubber cylinders can be extended
or compressed somewhat like the bellows of an
accordeon. The rubber is supported by iron rings inside,
placed from 4 to 6 inches apart, so as to prevent
them from collapsing when the air is exhausted from
them. When this is done the pressure on the movable
cast iron end draws it towards the fixed one, and by
attaching the former to the brake levers by a rod, the
force of the pressure on the head is communicated to
the brakes.
The ejector is placed on top of the boiler, and when
the brakes are to be applied the locomotive runner
opens a valve, which admits steam into the ejector,
which instantly begins to produce a partial vacuum
and thus apply the brakes. When the pressure of the
brakes is to be released, the release valve, D, is opened,
which admits air into the pipe, C, through which it is
conducted back to each of the India rubber cylinders,
and thus counteracts the pressure on the ends and releases
the brakes.
Both the atmospheric and the vacuum brakes have
recently been applied to the driving-wheels of locomotives
with very excellent results.
PART XXIV. PERFORMANCE AND COST OF OPERATING LOCOMOTIVES.
Question 445.What is the cost of operating ordinary
locomotives per mile run?
Answer. The average cost at the present time (1874)
is from 20 to 25 cents per mile.[103]
[103] Deducting 10 per cent. from this amount will give very nearly the
gold value of the cost. The figures given above represent the cost in
the depreciated promises to pay of the United States Government.
Question 446.What items of cost are included in this,
and what proportion do they each bear to the total cost?
Answer. The items of cost and the percentage of
each to the whole expense of operating locomotives,
and also to the total of all the expenses of operating
locomotives are given in the following table:
Approximate average cost per mile run.
Percentage of total cost of operating locomotives.
Percentage of total cost of all the operating expenses of railroads.
Fuel
6
.0 cts.
0
.30
.03
Oil and waste
0
.4 cts.
0
.02
.004
Wages of locomotive runners and firemen
6
.0 cts.
0
.30
.06
Repairs of locomotives
7
.0 cts.
0
.35
.07
Cleaning locomotives
0
.6 cts.
0
.03
.006
Total
20
.0 cts.
1
.00
.20
From this table it will be seen that the locomotive
expenses are 20 per cent. of the whole cost of operating
railroads. This cost of course varies under different
circumstances. The above is probably somewhat
lower than the average cost in this country.
Question 447.How many miles do locomotives ordinarily
run per ton of coal and per cord of wood?
Answer. This also varies greatly under different circumstances.
An average taken from the monthly reports
of 52 different roads gives 38 miles run per ton
of coal, and an average from the reports of 16 roads
gives 47¹⁄₂ miles run per cord of wood. No deductions
should, however, be made from this of the relative
value of wood and coal for fuel, because the trains
which are run with wood for fuel are usually lighter
than those hauled with coal-burning engines. The
above figures are the average results during the
month of May, 1871, of all the trains on the roads
from whose locomotive reports it has been compiled.
The following report of experiments, which were carefully
made by the writer, will give the performance
of a locomotive when great care is taken to produce
good results. It should be stated, however, that the
engine with which these experiments were made had
been in service eighteen months, without receiving
thorough repairs, and that the boiler at times primed
badly, so that the rate of evaporation of water per pound
of coal is not a fair indication of the performance of
the engine in that respect. The coal used was known
as Brazil coal, from Indiana, and in order to compare
the performance of two engines only lumps of coal
were used, so as to leave no room for question regarding
the relative amount of fine coal used by each engine.
The maximum grades on the road on which the
experiments were made were 30 feet per mile, and
the total ascent from the lowest to the highest point
on the road was 374 feet.
LOCOMOTIVE EXPERIMENTS.
1873.
1873.
1873.
Date of experiment
July 21.
July 28.
August 2.
Number of miles run
145
145
145
Number of cars hauled
41
31
41
Total weight of cars, lbs.
1,497,240
1,119,650
1,508,860
Total amount of coal burned, lbs.
8,676
5,102
7,221
Total am’nt of water consumed, lbs.
63,531
45,719
52,609
Water evaporated per lb. of coal, lbs.
7.32
8.02
7.04
Miles run per ton (of 2,000 lbs.) of coal
33.4
50.8
38.8
Coal consumed per car per mile, lbs.
1.45
1.13
1.21
Average speed, including stops, miles
11.1
13
13.8
Question 448.How can we determine the speed at
which an engine is running?
Answer. In the absence of any special instruments
for the purpose, by counting the number of revolutions
of the driving-wheels per minute,
then multiplying the length of their circumference
in inches by the number of their revolutions
per minute and the product by 60, and
dividing the last product by 63,360. The quotient
will be the speed in miles per hour. Thus,
supposing driving-wheels which are 61¹⁄₂ in. in diameter,
and whose circumference is therefore 193.2 in.,
should make 164 revolutions per minute, then 193.2
× 164 × 60 ÷ 63,360 = 30, (nearly) miles per hour.
PART XXV. WATER-TANKS AND TURN-TABLES.
Question 449.How are locomotive tenders or tanks
supplied with water?
Fig. 225. Scale ¹⁄₁₆ in. = 1 foot.
Answer. At suitable points, called water stations,
along the line of the road, large tanks or reservoirs are
located, which are filled either from a natural stream
which is higher than the tank and thus flows into
the latter, or else the water is pumped in, either
by hand or by horse, wind, water or steam power.
These tanks are usually, when there is room for them,
located near the track, as shown in fig. 225, so that the
water can be conducted by a spout, a, direct from the
tank to the man-hole of the tender. Communication
to and from this spout is opened and closed by a valve,
b, inside of the tank. The spout is usually attached
to the tank by a hinged joint, so that it can be lowered
to the tender and then raised up out of the way
of the engine and train. It is generally balanced by
a counterweight, suspended to one end of a rope,
which passes over a pulley and is fastened to the spout
at the other end. Such tanks are now generally made
of wooden staves like a tub or pail, and supported on
a heavy frame, c c c, made of wood, as shown in the
engraving, or on stone or brick masonry.
Fig. 226. Scale ¹⁄₁₆ in. = 1 foot.
When there is no room for the tank or reservoir
near the track, it is placed in any convenient position
at some distance from it, and the water is then conveyed
by an underground pipe to the place where the
locomotive must take water. At the end of this pipe
what is called a water-crane, fig. 226, is located. This
consists of a vertical pipe, A, with a horizontal arm,
B, which is made so as to swing around over the man-hole
of the tender when the latter is to be filled with
water. In some cases the horizontal arm alone swings
around, but in others the vertical pipe turns with the
horizontal one in a joint, C, underneath the surface of
the ground. The latter plan is thought to be preferable
to the first, as the pipe is less liable to freeze fast
in the joint when the latter is underground than when
it is exposed above. A suitable valve, D, is also attached
to the pipe below ground, so that the stream of
water can be turned off or on at pleasure by the
wheel E.
Question 450.What considerations should determine
the source from which a supply of water should be
drawn?
Answer. The first must of course be its convenience
to the point where the water is to be used; but more
attention should be given to the quality of the water
than it ordinarily receives, as the use of impure
water, or that which contains a considerable amount
of mud or solid matter mixed with it, or in suspension
as it is called, or has lime or other mineral substances
chemically combined with it, will very soon
coat the inside of the boiler with a covering of scale,
which is a very bad conductor of heat, and consequently
the boiler is much less efficient and much
more heat is wasted than if the heating surfaces were
clear. Besides this loss of efficiency, when boiler
plates are covered with non-conducting scale, they
are much more liable to be injured by the action of
the fire than when the water comes directly in contact
with the metal of the plates. Some water, too, has a
corroding effect on the metal of the boiler which is very
destructive.
Question 451.How can the relative amount of incrustating
substances in different kinds of water be determined?
Answer. The relative quantity of solid matter or mud
which is held in suspension can be at least approximately
determined by simply filling vessels, say large
clear glass bottles, with different kinds of water and
letting them stand for some time until the solid matter
settles to the bottom.
An easy method of precipitating the lime and some
other salts which are held in solution and which will
not settle until they are converted into a solid form is
the following: Dissolve in a goblet of pure water (distilled
or freshly caught rain water) two or three teaspoonfuls
of the oxalate of ammonia. Have equal
quantities, say a goblet-full of each of the waters to be
tested, ranged side by side and marked so as to be
identified. Into each of these goblets stir equal quantities
of the solution mentioned—about three teaspoonfuls
will be enough—and let them stand for a
day. The lime and some other salts will be precipitated
and fall to the bottom as a powder; and the
quantity of this precipitate in each glass will form a
very good index of its relative injuriousness in the
formation of scale.
When the oxalate of ammonia cannot easily be procured,
an experiment may be tried, in the same way,
by dissolving common white soap, or other pure soap,
in a goblet of pure water, and then stirring into the
glasses of water to be tested a few teaspoonfuls of this
solution. The comparative amount of lime in the
water will be shown by the amount of coagulated matter
which will be thrown down.[104]
Question 452.How are locomotives turned around
on the track?
Answer. The most common means employed for
that purpose is a turn-table, fig. 227. This consists of
two heavy beams made of wood, cast or wrought iron,
placed side by side and resting on a pivot in the centre,
on which they turn. They are placed in a circular
pit below the level of the track, so that when rails are
laid in the ordinary way on top of the beams they will
be exactly level with the track which leads up to the
pit. By turning the beams on the central pivot so
that the rails will come exactly in line with the permanent
track which leads up to the pit, the locomotive
can be run on the turn-table, which is then revolved
a half-revolution, which of course reverses
the position of the locomotive and brings it opposite
the permanent track so that it can be run off from the
table. In order to prevent the beams from tipping
down when the engine first runs on or off of the turn-table,
wheels are placed at their outer ends which run
on a circular track and bear any inequality of weight
that may be thrown on them if the locomotive is not
equally balanced on the central pivot.
Fig. 228. Scale ³⁄₃₂ in. = 1 foot.
Question 453.How is the central pivot constructed?
Fig. 227. Scale ³⁄₃₂ inch = 1 foot. 50-Foot Turn-Table, by William Sellers & Co., Philadelphia.
Fig. 229.
Answer. It usually consists of a vertical post, A,
shown in fig. 228, which is a transverse section through
the centre of the turn-table, the end of which rests on
hard cast iron or steel bearings. In some cases, as
shown in figs. 227 and 228, which represent a turn-table
built by William Sellers & Co., of Philadelphia,
the weight rests on conical steel rollers, m m, which
revolve in a circular path formed in the top plates.
Sometimes turn-tables are fitted with gearing and
cranks, D, fig. 228; but if they are made so that the
whole weight rests on the centre, and if they are of
sufficient length so that an engine and tender can be
moved on them sufficiently to be balanced over the
centre, gearing will not be needed; but a simple lever
fastened to the turn-table will be all that will be required
to turn the table and the engine and tender
on it. The tables should be of such a diameter or
length across the centre as will enable the class of engine
in use on any road to be balanced. With light
engines the 50-feet table is large enough; with the
long, heavy engine now used on the great trunk lines,
the engine and tender quite fill up the entire length
of 50 feet, leaving no margin for adjustment. In such
cases, the 54 feet, 56 feet, or, better, the 60 feet, should
be employed. These large tables are also made heavier
in proportion. The table should be of such a length
that engines, with tender either empty or full, when
run on the table can be so placed as to bring the centre
of gravity immediately over the centre. When so
balanced, one man can turn the loaded table with ease.
In setting up turn-tables it is necessary that the
foundation at centre, upon which the pivot rests,
should be of the most substantial character, so as not to
be liable to settle. The circular track, which may be
made of light rails, say 28 or 30 lbs. to the yard,
should be level, and the table should be so adjusted as
to swing clear of the circular track when loaded. The
pit required is quite shallow near the edge and deepens
towards the centre. Provision is made for covering
the entire pit by a platform turning with the
table, but this should be avoided whenever possible,
as the best constructed cover does offer some resistance
in turning. Even in roundhouses, where a covered
pit might be considered preferable as presenting
a smooth floor for crossing in any direction, it has
been found advisable, in view of the greatest ease
in turning and the facility offered by the open pit for
cleaning, to dispense with the cover. The centre
upon which the table turns is constructed of the best
cast steel, and consists of conical rollers of steel between
two steel plates grooved out to receive these
rollers. This part of the table must be kept clean and
well oiled, say with best sperm or lard oil and tallow
of such a consistency as not to harden in cold weather.
The top cap at centre is held in place by a circle of
bolts. These bolts take the entire weight of the table
and load; by slacking off the bolts the table can be
lowered on the wheels on the circular track and the
cap lifted off to gain access to the plates and rollers.
These should be opened, examined and cleaned at
least once every three months.
Under the cap and between it and the top of the
centre box are segments of wood. These can be altered
in thickness to bring the table in proper adjustment.
If the centre foundation settles, these segments
should be thinned sufficiently to enable the table to
be screwed up to a proper height. With proper care
such tables are practically indestructible.[105]
Question 454.Is there any other method of turning
locomotives?
Answer. Yes; what is called a Y is sometimes used.
This consists of a system of tracks laid somewhat in
the form of the letter Y, as shown in fig. 229, in which
A B is the main track, with two curves, A C and B C,
laid as shown. If now it is desired to turn a locomotive
which is standing in the position of the dart
A, it is run on the curve A C to the position of the
darts a and C. It is then run backward from C on the
curve C B, as represented by the dart b, and when it
reaches the main track in the position of the dart B
it is evident that its position will be reversed, as is
shown if we compare the direction of the dart A with
that of B.
PART XXVI. INSPECTION OF LOCOMOTIVES.
Question 455.What are the principal divisions of
the work of operating or running a locomotive?
Answer. They are: 1. Inspection and lubrication;
that is, an examination of the parts to see that they
are in good working order, and the application of oil
to the journals and other parts subjected to wear. 2.
Setting the engine in motion and starting the locomotive
and train. 3. Management while running. 4.
Stopping the engine and train. 5. Laying up. 6.
Management in case of accident. 7. Cleaning the engine.
Question 456.When the locomotive is inspected, what
should be especially observed about the boiler?
Answer. In the first place, all new boilers should be
tested by pressure before being used, and ALL boilers,
whether new or old, SHOULD BE TESTED PERIODICALLY.
The oftener the better. The ways of applying
the pressure test are: 1, the cold-water test, that
is, by filling the boiler with cold water and then forcing
in an additional quantity with a force-pump so as
to raise the pressure to that at which it is intended to
test the boiler; 2, the warm-water test, by filling the
boiler entirely full of cold water and then kindling a
fire in the grate so as to warm this water. As water
expands about one twenty-fourth in rising from 60 to
212 degrees, the rise in temperature will cause a corresponding
increase in pressure; 3, by steam pressure.
If the latter method were not so commonly used, it
would seem the height of madness to test a boiler—which
is neither more nor less than an attempt to
explode it—in the shop where it is built or repaired,
and where the results of an explosion would be more
disastrous and fatal than anywhere else, in order to
see whether it will explode when put into service
on the line of the road. The danger of explosion is
also increased at such times by hammering and caulking
at leaky rivets and joints.[106] It would seem, therefore,
very much more rational to test boilers first by
hydraulic pressure. For a first test this is preferable,
because cold water will leak through crevices which
would be tight when the boiler is heated, so that leaks
can be more surely detected with cold than with warm
or hot water. It is, however, doubtless true that boilers
are often strained much more by the unequal expansion
of the different parts than by the actual pressure.
It is therefore thought that after the hydraulic
test has been applied the second or warm-water test
should be used. This can be easily done, as the boiler
must be filled full of water for the first test. When
the boiler is subjected to the test pressure, it should
be carefully examined to see whether any indications
of weakness are revealed. Any material change of
form or any very irregular change of pressure is indicative
of weakness. The flat stayed surfaces should
be carefully examined by applying a straight edge to
them before and after they are subjected to pressure,
to see whether they change their form materially. One
of the greatest dangers and most common accidents to
locomotive boilers, as has been pointed out in a previous
chapter, is the breaking of stay-bolts, to detect
which, a locomotive runner and master mechanic
should exercise constant vigilance. While the pressure
is on, the outside surface of the boiler should be
thoroughly examined with slight blows of a hammer,
which will often reveal a flaw in the metal or a defect
in workmanship. After the hydraulic and warm-water
tests have been applied, the boiler should be
emptied, and the inside examined carefully to see
whether any of the stays and braces have been broken
or displaced by the test. After this has been done,
and not until then, should steam be generated in the
boiler. In making the latter test it would doubtless
be more safe to employ a pressure somewhat lower
than that employed with the cold and warm water.
There is great diversity of opinion regarding the maximum
pressure which should be employed in testing
boilers. It is doubtless true that a weak boiler might
be injured and thus made dangerous by subjecting it
to a very severe pressure, while without such a test it
would have been safe. Recent experiments have indicated,
however, that in most cases the ultimate
strength of material is actually increased by subjecting
it to a strain which even exceeds the elastic limit,
provided such a strain is imposed only a few times.
Although no absolute rule can be given to govern all
such cases, it is thought that for the hydraulic and
warm-water tests, a pressure about 50 per cent. greater
and for the steam test 25 per cent. greater than the
maximum working pressure should be employed.
Before old boilers are tested, they should be very
carefully examined, both inside and outside, to see
whether they are injuriously corroded. It is to be
regretted that the insides of locomotive boilers are
usually made so difficult of access that it is impossible
to discover the extent and the effects of corrosion
without the most careful examination. This is
not possible without getting inside of the boiler.
Whenever this can be done, a prudent locomotive runner
should use the opportunity of inspecting the boiler
of his engine himself, and not depend upon the boiler-makers
who are employed for that purpose. He
should remember that it is his life and not theirs
which is exposed to danger by any weakness or defect
in the construction of the boiler of the locomotive
which he runs.
Before starting the fire in a locomotive, the fire-box
should be carefully examined to see if there are any indications
of leaks, which will often reveal cracked plates,
defective stay-bolts or flues. If the latter simply leak
at the joints, they can generally be made tight by
caulking or the use of the tube expander. This is
easily done when the engine is cold, but if not attended
to may be very troublesome on the road. Leaks
at other parts of the boiler should be examined, as
they may reveal dangerous fractures.
It is of the utmost importance, both for safety and
for economy of working, that boilers should be kept
clean, that is, free from mud and incrustation. In
some sections of the country, especially in the Western
States, this is the greatest evil against which locomotive
runners and those having the care of locomotives
must contend. The cures which have been proposed
are numberless, but that which is now chiefly relied
upon is, first, the use of the best water that can be
procured, and second, frequent and thorough washing
out of the boiler.
Question 457.What sort of examination should be
given to the boiler attachments?
Answer. It should be observed whether the grate-bars
or drop-doors of the grate are properly fastened,
and whether the ashes have been cleaned out of the
ash-pan, and also whether the fire is clean, that is,
whether the grates are free from cinders or clinkers.
The height of water in the boiler should be observed
by testing it with the gauge-cocks and by noticing it
in the glass gauge, if one of the latter is used. It is
also well to blow out the sediment and mud from the
latter before starting, and to see that the valves which
admit steam and water to the glass are open. They
should, however, be opened only a very short distance,
so that only a small quantity of steam or hot water
will escape in case the glass tube should be broken.
The injector, if one is used, should be tested to see
that it is in working order, and as soon as the engine
starts out of the engine house both of the pumps
should also be tested, in order to see whether they are
in good working condition. The safety-valves should
be raised, so as to be sure that they are not rusted or
otherwise fastened to their seats. There is no part of
a locomotive more liable to disorder than the steam
gauge. For this reason it should be frequently tested,
and whenever there is any indication of irregularity
in its action it should be examined. As the wire netting
on the smoke-stack often has holes cut into it by
the action of the sparks, it should be frequently examined
to see whether it is in good condition. It is
also liable to be “gummed up,” especially if too much
oil is used in lubricating the cylinders and valves. As
soon as holes are cut into the netting there is danger
that the sparks which escape will set fire to the combustible
material near the track, and if the netting
is gummed up the draft will be obstructed and the engine
will not make steam. The gummy matter can
often be removed by building a wood fire on top of the
netting. In this way the oil in the gummy matter is
burned up, which leaves a dry material which can
then, at least to some extent, be beaten out of the
netting.
Question 458.How can it be known whether the
pumps are working well?
Answer. Their operation is indicated by the force of
the stream which escapes from the pet-cock when it is
open. When the pump is in good condition the water
begins to escape promptly in a strong stream as soon
as the pump-plunger begins its inward stroke, and
continues to escape until the plunger completes its
stroke. If the pump is not in good condition, this escaping
stream is weak and is apt to continue during
the outward stroke of the pump-plunger. It is difficult
to tell, however, when the engine is running
slowly, whether the pump will work well at higher
speeds, and therefore a locomotive runner should always
test the condition of the pumps during the previous
run.
Question 459.What should be noticed in connection
with the throttle-valve?
Answer. As a failure of the throttle-valve to work
may be the cause of a most serious accident, it should
be certain that it is in good working condition, that
all the bolts, pins and screws and other accessories are
in good working order. It should also be known
whether the throttle-valve is steam-tight. This can
be learned by observing whether steam escapes from
the exhaust-pipes or cylinder-cocks when the latter
are open, the reverse lever in full gear, and the
throttle-valve closed. If the throttle-valve leaks,
enough steam may accumulate in the cylinder, when
there is no one on the engine, to start it, and in this
way cause a serious accident. The throttle-lever
should always he fastened with a set-screw or latch of
some kind when the engine is standing still.
Question 460.In inspecting the cylinders, pistons,
guides and connecting-rods, to what points should the attention
be directed?
Answer. It should be known whether the piston
packing is properly set out, that is, whether it is so
tight that it will not “blow through,” or leak steam
from one end of the cylinder to the other, which of
course will waste a great deal of steam. Of the two
evils, it is, however, better to have piston-packing too
loose than too tight, because if it is too tight, it is liable
to cut or scratch the cylinders so as to make it
necessary to rebore them, and at the same time if the
packing-rings are lined with Babbitt metal, the heat
created by the intense pressure and friction will melt
the metal. In some cases the cylinders become heated
to so high a temperature from this cause that the
wood-lagging with which they are covered on the outside
is burned.
The packing of the piston-rods should be steam-tight,
and it should be observed whether the rod and
the pump-plunger are securely attached to the cross-head.
The utmost care must be exercised to keep the
guides well oiled. The oil cups on the guide-rods or
cross-heads, when they are placed on the latter, must be
kept clean, so that the oil will flow freely, and yet not
too rapidly, on the surfaces exposed to friction. The
same thing is true of the oil-cups on the connecting-rods.
Attention should be given to the brass bearings
of the connecting-rods to see that they are not so loose
as to thump, nor keyed so tight on the crank as to be
liable to heat. The latter can be easily known by
moving the stub-end lengthwise of the journal. They
should never be so tight that they cannot be thus
moved with the hand. Especial attention should be
given to seeing that all the bolts and nuts on the connecting-rods
are tight. There are no parts of a locomotive
which require more careful attention in order
to keep them lubricated, and thus prevent them from
heating and being “cut,” than the bearings on the
crank-pins and the slides of the cross-head. Examination
should be made to see that neither the piston-rods,
pump-plungers, guides, connecting-rods nor
crank-pins are bent or sprung.
Question 461.How can it be known whether the
piston-packing is too loose or “blows through?”
Answer. It can usually be noticed in the sound of
the exhaust, which can be heard very distinctly on the
foot-board when the furnace door is opened. If the
packing is not tight, it produces a peculiar wheezing
sound between and after each discharge of steam. If
the packing leaks, it will also be indicated by the escape
of steam from both the cylinder-cocks, if they are
open, just after the crank passes the dead point. This
will usually show in which of the cylinders the packing
is too loose. The same thing will occur, however,
if either or both of the main valves leak, so that it is
often hard to determine whether the “blow” is due to
a leak from the valve or from the piston. Of course,
it may sometimes happen that both leak, or that the
piston on one side and the valve on the other leak, so
that often the diagnosis of the disease, as the doctors
say, is extremely difficult. Careful observation and
experience will, however, aid a locomotive runner in
detecting such defects much more than any directions
which can be given here.
Question 462.What is meant by “setting out packing,”
and how should it be done?
Answer. “Setting out packing” is simply expanding
the rings when they get too loose. With ordinary
spring packing, figs. 96 and 97, which is now generally
used, this is done by screwing up the nuts b, b, b,
which, as was explained in answer to Question 169,
compresses the springs a, a, a, and thus expands the
rings A, A. In doing this, as already stated, great
care must be exercised not to screw the nuts up too
hard, and it is always better to have the packing too
loose than too tight. Care must also be taken to keep
the piston-rod in the centre of the cylinder, otherwise
there will be undue pressure and wear on the stuffing-box.
After the nuts are screwed up, the position of
the piston-head should be tested with a pair of callipers.
This is done by placing one leg of the callipers
against the side of the cylinder, and setting them so
that the other leg will just touch the edge of the projection
E, fig. 96, or the end of the piston-rod. Then
by placing the callipers above and below, and on each
side of the piston, it will appear whether it is too high
or too low or too near either side; then by loosening
the nuts on one side and tightening them on the other
it can be moved to a central position. Ordinarily this
work is intrusted to persons who are employed for the
purpose. A young locomotive runner, fireman or mechanic
will, however, always do well to familiarize
himself with such duties, and, if possible, do it himself,
under the direction of those who are skilled in
that kind of work.
Question 463.If the stuffing-box of the piston-rod
leaks, what should be done?
Answer. If the packing in it is in good condition,
it can usually be made tight by simply screwing up
the gland. In doing this, the nuts on the bolts should
not be screwed up more than is necessary to make the
packing steam-tight. Any greater pressure only increases
the friction on the piston-rod unnecessarily.
In doing this, the two bolts must be screwed up
equally, otherwise the gland will be “canted,” that is,
inclined so as to “bind” or bear unequally and very
hard against the piston-rod, and thus be liable to cut
or scratch it. After packing has been in the stuffing-box
a long time, it becomes very hard and compact,
and sometimes partly charred. Then either it must
be removed and new packing be put in, or, if in tolerably
good condition, it can often be made to work
well by simply reversing it, that is, by putting that
which was at the bottom of the stuffing-box on top
and vice versa. Before packing is put into a stuffing-box,
the former should always be thoroughly
oiled.
Question 464.When the slides of the cross-heads
wear, how is the lost motion taken up?
Answer. When there are gibs on the cross-head,
the lost motion can be taken up by putting “liners”
or “shims,” that is, thin pieces of metal, between them
and the cross-head, so that they will fill up the space
between the guide-bars. When there are no gibs, the
guide-bars must be taken down, and the blocks between
them at each end must be reduced in thickness
so as to bring the bars nearer together. In doing this,
great care must be taken that the guides are accurately
“in line” with the centre line or axis of the
cylinder. This work should never be intrusted to any
excepting skilled workmen, from whom those who are
inexperienced should seek instruction.
Question 465.When the brass bearings of the connecting-rods
become too loose on their journals, what should
be done?
Answer. They must be taken down, and the two
surfaces in contact must be filed away so as to bring
them closer together. In doing this they must be
filed square with the other surfaces, otherwise they
will not bear equally on the journals when they are
keyed up. Before attaching them permanently to the
rods, they should be keyed on the journal in the strap
alone, so that it can be known by trial whether they
move freely and yet are tight enough to prevent
thumping on the journal. When they are attached to
the rod, it is very important, especially with coupling
or parallel-rods, that the correct length from centre to
centre of the bearings be maintained. It is much better
to leave coupling-rods loose on their journals, because,
if the bearings are keyed up tight, the rods are
sure to throw an enormous strain on the crank-pins,
as the distance between the centres of the axles is not
always absolutely the same, owing to the rise and fall
of the axle-boxes in the jaws. It is therefore always
best to have a little play in the coupling-rods, and it
is safe to say that much more mischief is done by meddling
with the coupling-rod brasses than by neglecting
them.
Question 466.What part of the valve gear should
receive attention when the engine is inspected?
Answer. All the bolts, nuts and keys should be carefully
examined to see that they are properly fastened.
The bolts and nuts in the eccentric straps are especially
liable to become loose, and as they are between
the wheels, and therefore not easy of access, are often
neglected. The oil-holes should all be seen to be clear,
otherwise it will be impossible to keep the journals
well oiled. The eccentric straps and the link blocks
are very liable to be imperfectly oiled, and when the
former become dry and cut, they throw a great strain
on the eccentric-rods, which is liable to break them.
When this occurs the strap and the portion of the rod
which is attached to it revolve with the eccentric, and
frequently a hole is thus knocked into the front of the
fire-box, which disables the engine. The valve gear
is, with the exception, perhaps, of the pumps and injector,
the most delicate part of the locomotive, and
more liable to get out of order than any other, and
should therefore be watched with the greatest care.
Question 467.How can it be known whether the main
valves of a locomotive are tight?
Answer. As already indicated, the symptoms which
manifest themselves when a valve leaks are very similar
to those which appear when the piston packing
leaks. If the valve is moved to its middle position
and steam is admitted into the steam-chest, and it
then escapes from both cylinder-cocks, it is apparent
that the valve is not tight. But the valve faces of
locomotives usually wear concave, because the valves
are worked most about half-stroke, so that they will
often be tight when in the centre of the face, but will
leak at the ends of the full stroke. This will become
apparent by the peculiar wheezing sound, already referred
to, when the engine is at work. As has been explained,
it is, however, often very difficult to determine
whether this sound is due to a leak at the pistons or
the valves. If the packing of the valve-stem leaks, it
can be remedied in the manner described for making
that of the piston-rod tight.
Question 468.To what points of the running gear
should attention be directed during inspection?
Answer. All the wheels of the engine and tender
should be carefully examined to see that they are
sound. A fracture in a driving-wheel is usually apparent
if the wheel is carefully examined. The condition of
ordinary cast iron tender and truck-wheels is revealed
on striking them with a hammer, when if they are
sound they will give out a peculiar clear ring; whereas
if they are fractured, the sound produced by the blow
of the hammer will be dead, like that of a cracked bell.
The flanges of the wheels should also receive attention
to see that they are not broken, as such a fracture is not
always revealed by the sound produced by a blow from
a hammer. The axles too should be examined to see
that the wheels have not worked loose on the wheel-seat.
When this occurs it often becomes apparent by
the oil from the axle-boxes working through between
the hubs of the wheel and the axle. This can be observed
on the outside of the wheels when the bearings
are inside, and inside the wheels when the bearing
is outside.
The springs should be examined to see that they
are in good condition, and the oil-holes in the boxes
must be kept clear, so that the oil can reach the bearings.
The tender boxes are kept oiled by packing
them with cotton or woolen waste saturated with oil.
This should be taken out occasionally and renewed
and the boxes cleaned. The working of the driving-boxes
up and down the jaws will in time wear them
so that there will be some lost motion in the jaws.
This will be indicated by a thump when the cranks
pass the dead point. A similar thump will, however,
be produced by lost motion in the boxes of the main
connecting-rod, so that it is difficult to determine,
without special examination, the cause which produces
the concussion. It is therefore best when an engine
works with a thump at each revolution for the runner
to stand by the side of it where he can touch the connecting-rods
and driving-wheels, and then have the
fireman open the throttle-valve so as to move the engine
slowly. If the lost motion is in the connecting-rods
it can be felt by the jar as it passes the dead
points. The same is true of lost motion in the jaws,
which can be felt by touching the driving-wheels.
When the jaws become worn the lost motion can be
taken up by moving up one or both of the wedges.
When this is done, great care must be taken to keep
the centres of the driving-axles the same distance
apart on both sides of the engine, and also to keep
their centre lines square with the frames. There
should always be centre-punch marks placed on the
frames or guide-yokes on each side of the engine in
front of the main axle, and at equal distances from its
centres, so that when the boxes or jaws become worn
the position of the axle can be adjusted with a tram
from these marks. Of course, if the main axle is
square, it is easy to adjust the trailing axle from it
with a tram. If the axles are not square with the
frames and parallel with each other, the engine will
run towards one side or the other of the track, according
to the inclination of the axles. It sometimes
happens that the bolts which hold up the wedges in
the jaws are broken. When this occurs the wedge
drops down, and of course the box has so much lost
motion that it soon manifests itself in the working of
the engine. These bolts, and also those which hold
up the clamps on the frames at the bottom of the jaws,
should be examined when the engine is inspected, so
as to be sure they are in good condition. The bolts
and nuts about both the engine and tender trucks
should be watched to see that none are lost or work
loose. The engine and tender should occasionally be
lifted up from the centre plates of the truck, and the
latter be lubricated with tallow. It often happens
that these become dry, so that they are difficult to
turn when the weight rests on them, and therefore
they will not adjust themselves easily to the curves of
the track.
Question 469.What other parts of a locomotive
should be examined before starting?
Answer. It should be certain that the brakes on the
tender are in good working condition, that is, that the
bolts, nuts and keys are all secure, the levers, rods
and chains properly connected, and the shoes fastened
and not too much worn. If either an atmospheric or
vacuum brake is used, it should be tested before starting,
to see that the pump or ejector is in good working
condition. It is also well to apply the brakes to
the train before starting, so as to see whether the connections
are in good condition and properly connected.
It is always best for the locomotive runner to examine
the connections of the brake hose through the whole
train himself, to be sure that they are properly made.
The inside of the water-tank should also be examined
occasionally, to see whether it is clean, and if not it
should be thoroughly washed out. The man-hole
should always be covered before starting, in order to
prevent cinders and coal from falling in, which are
liable to obstruct the pump valves. It is hardly necessary
to say that it must always be certain before
starting that there is enough water in the tank to feed
the boiler until the next point is reached at which a
supply can be obtained. The sand-box must also be
filled, the bell rope in good condition, and if running
at night the reflector of the head-light must be polished
and the lamp supplied with oil and the wick
trimmed so as to burn brilliantly. The locomotive
runner must also see that the proper signals are displayed
in front of his engine.
Question 470.What tools, etc., should every locomotive
runner on the road carry?
Answer. A coal shovel, coal pick, long-handled hoe[107]
and poker, a pair of jacks, either screw or hydraulic,
chains, rope and twine to be used in case of accident,
a heavy pinch-bar for moving the engine, a small
crow-bar, oil-cans with short and long spouts and another
smaller one with spring bottom, a steel and a copper
hammer, a cold and a cape chisel, a hand-saw, axe
and hatchet, one large and one small monkey-wrench
and a full assortment of solid wrenches for the bolts
and nuts of the engine, cast iron plugs for plugging
tubes, with a bar for inserting them, two sheet iron
pails or buckets, different colored lanterns and flags,
according to the colors used for signals on the line,
and a box with a half-dozen torpedoes.
[107] These are of course not needed on wood-burning engines.
Question 471.What duplicate parts should be carried
with the engine?
Answer. Keys, bolts and nuts for connecting-rods,
split-keys, wedge bolts, bolts for oil-cellars of driving
and truck boxes, driving and truck spring-hangers,
wooden blocks for fastening guides in case of accident,
blocks for driving-boxes and links, a half-dozen ³⁄₄-in.
bolts, from six inches to two feet long, to be used in
case of accident, two extra water-gauge glasses, two
glass head-light chimneys.
Question 472.What should be observed in lubricating
a locomotive or any other machinery?
Answer. The most important thing to observe is
that the oil reaches the surface to be lubricated. It
is of much greater importance that the lubricant
should reach the right place than that a large quantity
should be used. A few drops carefully introduced
on a journal will do much more good than a large
quantity poured on the part carelessly. For this reason
all oil-cups and oil-holes should be kept clean so as to
form a free passage for the oil.
PART XXVII. RUNNING LOCOMOTIVES.
Question 473.Before starting the fire in a locomotive,
what must be observed?
Answer. It must always be noticed, before kindling
the fire, whether the boiler has the requisite quantity
of water in it; that all cinders, clinkers and ashes
are removed from the grates and ash-pan; that the
grates and drop-door are properly fastened, and that the
throttle-valve is closed and the lever secured. Locomotive
boilers are sometimes seriously injured by
building a fire in them when there is no water in the
boiler. In filling a boiler it must be remembered,
however, that when the water is heated it will expand,
and that when bubbles of steam are formed they will
mix with the water and thus increase its volume, so
that after the water is heated its surface will be considerably
higher than when it is cold.
Question 474.How should the fire in a locomotive be
started?
Answer. It should be started very slowly, so as not
to heat any one part suddenly. Probably the greatest
strains which a locomotive boiler has to bear are those
due to the unequal expansion and contraction of its different
parts. When the fire is started, of course the
parts exposed to it are heated first, and consequently
expand before the others. Now, if the fire is kindled
rapidly, the heating surfaces will become very hot before
the heat is communicated to the parts not exposed to
the fire. Thus the tubes, for example, will be expanded
so as to be considerably longer than the
outside shell of the boiler, and therefore there will be
a severe strain on the tube-plates, which will be communicated
to the fire-box, stay-bolts, braces, etc.
The inside plates of the fire-box will also become
much hotter than those on the outside, and as it is rigidly
fastened to the bar to which both the inside and
the outside shells are fastened at the bottom, its expansion
will all be upward, which thus strains the stay-bolts
in that direction. As the motion due to this expansion
is greatest near the top of the fire-box, the
top stay-bolts are of course strained the most, and it
is those in that position, as has already been pointed
out, which are the most liable to break. When steel
plates are used the expansion or contraction often
cracks them, and sometimes, hours after the fire is
withdrawn from the fire-box, the inside plates will
crack with a report like that of a pistol. It is therefore
very important both to heat and cool a locomotive
boiler very slowly, and the fire should always be kindled
several hours before the engine starts on its run.
Question 475.What should be done when the locomotive
leaves the engine-house and before the train is started?
Answer. Before leaving the engine-house the cylinder
cocks should be opened, so that all the water or
steam which is condensed in warming the cylinders
can escape. Before the engine is started from the
engine-house the bell should be rung and time enough
allowed for any workmen employed about the engine
to get out of the way. This rule must be scrupulously
obeyed under all circumstances, and a locomotive should
never be started without first giving such a signal.
Without it there is always danger that some one
about the engine will be hurt or killed. While running
from the engine-house to the train the runner
should observe very carefully the working of all the
parts of his engine, and as far as possible see that they
are in good working condition. The fireman should stay
on the tender to handle the brake, as may be necessary,
and should assist in coupling the tender to the
first car of the train. The junction with the train, especially
when it is a passenger train, should be made
very gently, as otherwise passengers may be injured
by the shock. Before starting the runner should see
himself that the engine and tender are securely coupled
together, and the latter to the train, that the frictional
parts are properly lubricated, as explained heretofore,
that the fire is in good condition and that the
requisite quantity of steam has been generated. If
the steam is too low, the blower is started, which
stimulates the fire.
Question 476.When the train is ready, how should
the engine be started?
Answer. After the signal to start is given by the
conductor, the runner also gives a signal by either
ringing the bell or blowing the whistle. The latter
should, however, be used, especially at stations, as
little as possible, on account of the risk of frightening
horses and the shock which it produces on persons
who are unaccustomed to hearing it, or are suffering
from any nervous disorder. After giving the requisite
signal, the runner places the reverse-lever so that the
valve will work either in full gear or very near it.
He then opens the throttle slowly and cautiously so as to
start the train gradually. If the train is a very heavy
one, it is best to back the engine so as just to “take
up the slack of the train,” that is, to push the cars together
so that there will be no space between them
and thus compress the car draw-springs. When the
cars stand in this way, those at the front end of the
train are started one after another, which makes the
start easier than it would be if it were necessary to
start them all at once. If the throttle is opened too
rapidly, the driving-wheels are apt to slip, but with a
very heavy train, even with the greatest care, this is
liable to occur. If the train can not be started otherwise,
the rails must be sanded by opening the valves in
the sand-box. As little sand should be used as possible,
because the resistance of cars running on sanded
rails is greater than on clean rails, and thus the train
is more difficult to draw after it reaches the rails to
which sand has been applied. Thus the difficulty to
be overcome may be increased by the means employed
to overcome it.
While the train is slowly set in motion the fireman
and runner must ascertain by watching whether the
whole train moves together, and that none of the couplings
are broken in starting, and also whether any
signal is given to stop, as is sometimes necessary
after the train has started. On leaving the station
he should observe whether all the signals indicate that
the track is clear and that the switches are set right,
and also look out for obstructions on the track. The
train should always be run slowly and cautiously until
it has passed all the frogs, switches and crossings of
the station yard, and not until then and when the
runner has seen that everything is in order should he
run at full speed. As the engine gains in speed the
reverse lever should be thrown back and nearer the
centre of the quadrant or sector, so as to cut off
“shorter.”
Question 477.After the engine is started, how can
it be run most economically?
Answer. The advantage of using steam expansively
has already been explained in Part V.; it is more
economical to use steam of a high pressure which is
done by keeping the throttle-valve wide open, and
then regulating the speed by cutting off shorter—that
is, expanding it more. If the speed is reduced by
partly closing the throttle-valve, the steam is wire-drawn
and, as was shown in answer to Question 59,
it then produces much less useful effect than it would
if it was admitted into the cylinder at full boiler
pressure.
It is found, however, that in many cases if the
steam is cut off very short the final pressure when it
escapes is so low that it does not produce blast enough
to stimulate the fire, and therefore the boiler will not
make enough steam. This is more liable to occur
with engines which have small than with those which
have large boilers, or when the boilers are in bad condition
or the fuel is of poor quality. When it does
occur it is necessary to work steam during a longer
portion of the stroke, so as to increase the final pressure
when it is exhausted and regulate the speed with
the throttle-valve. Of course this is very wasteful,
but it is often the best which can be done and pull the
train.
There is also another practical difficulty in using
steam of a high pressure and running with the throttle
wide open and regulating the speed with the reverse
lever alone. The link motion, as has already
been explained, will not be effective in cutting off at a
point below about one-quarter of the stroke. Now it
often happens, even when cutting off at that short
point, with light trains on a level or slightly descending
grade, that the speed will be too great if the
throttle is wide open and with full steam pressure in
the boiler. When this is the case, it is absolutely
necessary to reduce the speed either by partly closing
the throttle, or reducing the pressure in the boiler.
Undoubtedly if valve-gear for locomotives was so constructed
that steam could be cut off effectively at a
shorter point of the stroke, it would result in increased
economy in the use of steam.
The runner should aim to run at as nearly uniform
speed as possible, and in order to do so should divide the
distance between stopping points and the time given
for running it into as small divisions as he conveniently
can, so as to be able to tell as often as possible
whether he is running too fast or too slow, and thus
travel over the shorter spaces in corresponding periods
of time.
Question 478.How should the boiler be fed?
Answer. The feeding of the boiler should if possible
be continuous, and the quantity of water pumped into
it should be adjusted to the amount of work which the
engine is doing. Ordinarily one pump is more than
sufficient for feeding the boiler, so that usually only
the one on the right side of the engine, where the
runner stands, is used. The flow of the water is regulated
by partly opening or closing the feed-cock. The
injector is commonly used only when the engine is
standing still, when the pumps will not feed. In feeding
the boiler it must be seen that the water is neither
too high nor too low. If it is too low there will be
danger of overheating the crown-plates or even of an
explosion; if it is too high, the steam space in the
boiler is diminished unnecessarily, and will cause the
water to rise in the form of a spray, and thus be carried
into the cylinders with the steam, or the boiler
will prime or foam, as it is called. This water, if it
collects in the cylinder as already explained, may by
the concussion produced by the motion of the piston
break the cylinder.
Question 479.What is the cause of priming in a
boiler?
Answer. It is often caused by the difference in temperature
and pressure in the water below and the
steam above. Thus, if we have a boiler in which the
water is heated to a temperature due to 100 lbs. effective
pressure, or 338 degrees, and we then open the
throttle-valve suddenly, so as to relieve the pressure
on top of the water, there will at once be a rapid generation
of steam in the water which will rush to fill
the space from which the steam has been drawn. This
newly generated steam will be formed at the hottest
part of the boiler first, that is, next to the heating
surface. It will therefore happen that as soon as the
pressure is relieved, bubbles of steam from all parts of
the heating surface of the boiler will flow to the point
at which the steam escapes. The motion of these
bubbles will be so rapid that large quantities of water
will be carried with them. The same thing will also
occur if the heat of the water is increased very rapidly.
The water will then become hotter than the temperature
due to the pressure of the steam above it, and
consequently there will be a rapid formation and escape
of bubbles of steam from the water, which will
thus have the same effect as they would have if the
steam pressure was reduced.
The amount of water carried up with the steam is
increased if the escape of the latter is obstructed in
any way, owing to imperfect circulation of water in
the boiler, or by floating impurities, such as oil, on the
surface. When this condition of things exists, the
ebullition is, as it were, convulsive, and the water is
thus carried up with the steam when it escapes.
Priming is also probably due in some measure to the
flow of steam over the surface of the water to the point
of outflow,[108] carrying particles of water with it just as
a high wind will, when blowing over the crests of the
waves of the sea.
When steam is drawn, as it usually is in locomotives,
from the top of the dome to which the safety-valves
are attached, the tendency to prime is very
much increased when they are blowing off, so that
some engineers advocate the use of two domes, from
both of which the supply of steam is sometimes drawn,
and in other cases the safety-valves are mounted on
one, and the steam-pipe is placed in another dome.
Whenever the safety-valves begin blowing off steam,
the pressure in the boiler should be reduced as soon
as possible, not only because when they are blowing
off it tends to produce priming, but because the steam
which escapes from them is wasted. The pressure
can be most economically reduced either by increasing
the amount of water which is fed into the boiler or by
opening the heater cocks and allowing the steam to
escape into the tank and thus warm the water. If
the boiler is too full, the former method cannot be
employed, and in heating the water in the tank the
runner must be careful not to get it too hot, because
in that case neither the pumps nor the injectors will
work satisfactorily, and the paint on the tenders is
also liable to be blistered and destroyed by the heat.
By feeling the tank with the hand it can soon be discovered
whether the water is too hot. If the steam
pressure cannot be reduced in any other way, the furnace
door must be partly opened.
The use of muddy water will also sometimes cause
a boiler to prime. It is probable that priming is
sometimes due to the formation of foam on the surface
of the water, and therefore all priming is often called
foaming; whereas it is thought that often a boiler
will prime when the water does not foam. More accurate
information regarding the priming of boilers is,
however, much needed, as many of the phenomena
have thus far not been satisfactorily explained. The
principal causes of priming in ordinary practice are,
however, undoubtedly owing to defective circulation,
too little steam room, impure water, or too much
water in the boiler.
Question 480.How can it be known whether an engine
is priming, and what should be done to prevent it?
Answer. The priming of a boiler can be known by
the white appearance of the steam which escapes from
the smoke-stack and the cylinder cocks. Dry steam
always has a bluish color. When an engine primes
or works water into the cylinders, it is usually
indicated by a peculiar dead sound of the exhaust,
which from this cause loses its distinctly defined and
sharp sound. This can be observed best when the furnace
door is opened. It is also indicated by the discharge
from the gauge-cock, as the water which then
escapes from the lower cocks is mixed with steam, or,
as runners say, is not “solid,” and the steam from the
upper cocks is not clear, but mixed with water. To use
a phrase employed by practical men, the priming or
foaming of the boiler may be known by the “flutter”
of the gauge-cocks. As soon as there are any indications
of priming, foaming, or that water is working
into the cylinders, the cylinder cocks should be opened
at once, otherwise the cylinders, cylinder heads or
pistons may be broken. The throttle-valve should be
either partly or entirely closed. When the latter is
done the foaming will in most cases cease for the time,
so that the runner can tell how much solid water there
is in the boiler. If he finds that the boiler has too
much water in it? it is best to shut off the pumps, and
in many cases the blow-off cock is opened. The latter
is, however, attended with some danger, because
if any obstruction should get into the blow-off cock, or
it should stick fast, so that it could not be closed, all
the water would escape from the boiler, and with a
heavy fire in the fire-box there would be great danger
of overheating, and thus injuring the boiler or of
“burning” it, as it is ordinarily termed.
A much better method of affording relief in such
cases is to place what is called a surface-cock in the
back end of the fire-box, about half way between the
upper and lower gauge-cocks. With such a cock, the
water can be blown off from the surface instead of
from the bottom. As foaming or priming is often
caused by oil, or other floating impurities on the surface,
they can be blown out of the boiler with this arrangement,
whereas, if the water escapes from the
bottom of the boiler, the floating impurities will
always remain after it is blown off. A perforated
pipe, which extends for some distance along the surface
of the water inside the boiler, is sometimes attached
to the surface-cock, so that the water which is
blown off will be drawn from a number of points along
the surface.
If the steam is rising rapidly when foaming begins,
it will be well to cool the boiler off by opening
the furnace door part way. This means of relief
should, however, be used as little as possible, because
there is always danger of causing the tubes or other
parts of the boiler to leak, by either heating or cooling
suddenly or rapidly. If the engine primes when there
is but little water in the boiler, and at a time when
the steam is rising rapidly, it may sometimes be remedied
by increasing the amount of feed-water, and thus
partly cooling the water inside. The use of pure
water, careful firing so as to keep the steam pressure
regular, feeding the boiler so that the level of the
water will be nearly uniform, and then starting the
engine carefully, that is, opening the throttle-valve
gradually, are the most effective means in practice of
preventing a locomotive boiler from priming.
Question 481.What is the economical effect of priming
on the consumption of fuel in locomotives?
Answer. It causes a great waste of heat, first by the
escape of that contained in the hot water which passes
through the cylinders and which does no work, and
second, when steam is mixed with a great deal of
water, it will not flow either to or from the cylinders
as quickly or easily as dry steam will. Consequently
the initial pressure on the piston, if the engine is running
even moderately fast, and is cutting off short,
will not be so great as it would be if dry steam was
used. Wet steam is also more difficult to exhaust
from the cylinder than that which is dry, and therefore
the back pressure on the piston is greater when
the boiler primes than when dry steam alone is used.
Question 482.When running on the open road, what
should the locomotive runner observe?
Answer. Either he or the fireman should constantly
watch the track in front of them, and also observe,
from time to time, whether the train of cars, especially
if it is a long one which he is handling, is in good
condition. He must observe every signal scrupulously,
and should never pass one until he
is sure that he is authorized to do so. The
well-known maxim, “be sure you are right; then go
ahead,” should be changed for locomotive runners to,
DON’T GO AHEAD UNTIL YOU ARE SURE YOU ARE
RIGHT, AND WHEN IN DOUBT ALWAYS CHOOSE THE
SIDE OF SAFETY. In running through curves, the
speed of the train should always be moderated in proportion
to the sharpness of the curve, and before reaching
it. In running through curves, the tendency of
the train is to continue in a straight line, and there is
thus danger of running off the track. The higher the
speed, of course, the greater is the resistance which is
required to prevent the train from running in a
straight line, and consequently the greater is the
strain which is thrown on the flanges of the wheels
and on the rails and axles. In running through
curves, it is also impossible, usually, to see further
than a short distance ahead, and therefore, if the train
is running very fast, it cannot be stopped in time,
should there be any obstruction or danger on the
track.
Question 483.What precautions should be observed in
running over steep grades?
Answer. On approaching an ascending grade the
runner should see that the fire is in good condition,
and as much coal should be put on it as can be burned
to advantage. He should also fill the boiler as full of
water as he safely can, without danger of priming, and
should heat this water as hot as possible without blowing
off steam at the safety-valves. The object of this
is to have a supply of water already heated before
reaching the grade. If, as often happens with a heavy
train, the boiler will not make as much steam as the
engine consumes, if there is a large supply of hot
water in the boiler it can be used as a reserve, should
it be necessary to do so, without danger of injury to
the boiler. If there was so little water in the boiler
that it would be dangerous to allow it to get lower,
then it would be necessary to feed cold water as rapidly
as the hot water escaped in the form of steam.
It is often impossible to heat all this cold water as fast
as it is pumped into the boiler, without reducing the
steam pressure until there is then not sufficient power
to pull the train. If, however, there is a supply of hot
water in the boiler, at the critical point on the grade,
where the engine is most liable to fail, the pump can
be partly shut off, and thus less water will be pumped
into the boiler, and the steam pressure be maintained
without danger. Undoubtedly it is better to feed locomotive
boilers uniformly, if that is possible, but it
often happens that a reserve supply of hot water in
the boiler enables an engine to pull a train up the
most difficult place, whereas, without such a supply,
the locomotive would stick fast. As the capacity of
locomotives is rated on nearly all roads by the number
of cars they can “pull up the hill,” of course whatever
aids them at the critical point increases their capacity.
It is this fact which gives engines with large
boilers so much advantage over those with small ones.
In running up steep grades, allowance should always
be made for the effect of the inclination of the track
upon the position of the water surface in the boiler,
and also the fact that as soon as the throttle-valve is
closed, and steam shut off, the surface of the water
will be considerably lower than when the engine was
working hard. On a grade of 50 feet to a mile, the
front end of the tubes of an ordinary locomotive would
be about 1³⁄₄ inches higher than the back end of the
crown-sheet. If, then, on working hard up such a
grade, it is succeeded by another of equal descent, the
front ends of the tubes would be 1³⁄₄ inches lower than
they were while coming up, so that if the back end of
the crown-sheet was covered with 1³⁄₄ inches of water
just before reaching the top, it would be exposed to
the fire as soon as the engine reached the descent.
This exposure would be dangerous, because not only
would the water be 1³⁄₄ inches lower over the crown-sheet,
but it would fall considerably more when the
throttle-valve was closed. These considerations will
show the danger of running the water too low while
ascending steep grades.
In pulling trains up steep grades, especial caution
should be exercised to prevent any of the cars from
breaking loose from the train, because such an accident
may cause great disaster.
As soon as the engine reaches the top of the grade,
the fireman should oil the main valves, because it can
only be done when steam is shut off, as the oil will
not run into the steam-chest when there is a pressure
of steam in it; and as the valves are always subjected
to the severest wear while pulling up a steep grade,
the valves and valve-faces are apt to become dry. As
saturated steam to some extent prevents valves from
cutting, it is not so important that they be lubricated
while the engine is working with steam, but as soon
as steam is shut off they should be oiled, otherwise
there is danger of their being injured by their friction
on the valve-seats.
In running down grades, the runner has the greatest
possible cause for using every precaution, because
not only is the train much more difficult to control, but
usually frequent sharp curves prevent a view of the
track for any considerable distance ahead. He should,
therefore, watch the track in front of him with the
greatest vigilance, so as to be ready to give the requisite
signals to the brakemen to apply the brakes, or, if
the engine and train are provided with continuous
brakes, to apply the latter, or even reverse his engine,
in case of danger.
Question 484.How should an engine be run past
those stations where the train does not stop?
Answer. The speed of the train should be slackened
in passing stations, especially if a clear view of the track
and switch signals can not be obtained at some distance
before reaching the station. There is always a
possibility that the switches may be turned wrong, or
that there may be some obstruction on the track at
stations, so that some caution should be exercised in
running past them. The proper signal, either by the
whistle[109] or the bell, should be given on approaching
stations, and also at all common road crossings.
[109] The methods of giving signals vary so much on different roads that
no general direction that will suit all cases can be given.
Question 485.What must be done on approaching a
draw-bridge or a crossing of another railroad at the same
level?
Answer. In many of the States it is provided by
law that all trains must come to a dead stop before
crossing a draw-bridge or another railroad at the same
level. Whether such a law exists or not, the rule
should always be observed. After coming to a stop,
the train should under no circumstances be started
until the signal has been given to start the train by
the signal-man at the bridge or crossing. A runner
should never assume that the signal has been given,
nor take another person’s word for it, but should see
and know it himself. In some conditions of the
weather and with the light falling on a signal in certain
directions, it is sometimes difficult to determine
its color or form. If there is any doubt about it, the
testimony of another person should always be sought.
There is good reason for believing that color-blindness,
that is, an incapacity for distinguishing one
color from another, is a much more common infirmity
than is usually supposed. It is certain, too, that
people who ordinarily distinguish colors very accurately
are subject to color-blindness in certain conditions
of health, and that it is sometimes the result of
overwork or great weariness; and a case is recorded
of a person who was always color-blind after a debauch.
There are, therefore, good reasons why a locomotive
runner should not always place too implicit
confidence in what he “sees with his own eyes,” but
if he has any doubt, he should take the “benefit of
the doubt,” which should always lead him to take the
side of safety.
Question 486.How should the engine and train be
managed in running into a station?
Answer. First of all when running into a station
when the train stops, the speed must be checked so
that the train will not enter with very great momentum.
Therefore, at a distance varying from one to
three-quarters of a mile, according to the nature of
the grades and track, the steam should be shut off, so
that the speed will be reduced so much that the train
under any circumstances will be under full control.
It is always better to enter a station at too low a speed
than to run in too fast, because if it is necessary, more
steam can always be admitted to the cylinders to increase
the speed before coming to a stop; whereas it
is not so easy to stop the train if it is running too
fast, and it becomes necessary to check it before entering
the station. This will sometimes be necessary,
because it may readily happen through negligence or
accident at stations that in switching cars one or
more may be left standing wholly or partly on the
track, which the arriving train must run over, in
which case a collision with its terrible consequences
may be unavoidable.
When a train is equipped with continuous brakes,
the control which they usually give to a locomotive
runner over the train is so great that he is apt to approach
stations, crossings or draw-bridges at a high
rate of speed, and rely on such brakes to stop the
train. This practice is always attended with great
danger, because if it was found, on getting near to the
station, crossing or draw-bridge, that the track was
not clear, and that it was obstructed by a car or train,
or the draw was open, if the runner should attempt
to apply the brakes and from some cause they should
fail to work, as sometimes occurs, then a collision or
other disaster would be inevitable, because it would
be impossible to stop the train with the ordinary hand
brakes. For this reason a locomotive runner should
always approach such places cautiously and with his
train under sufficient control, so that if he finds there
is danger ahead he can stop the train with the ordinary
means, or at the worst by reversing the engine.
Continuous brakes should always, excepting in cases
of imminent danger, be applied gradually, so as not
to check the cars with a jerk or too suddenly. The
practice of opening the cock which admits air to
atmospheric brakes suddenly, and then turning it
back again as quickly, is almost sure to produce disagreeable
and dangerous shocks to the cars. The cock
should be opened gradually, so as to check the cars
slowly at first.
Question 487.What must be attended to when running
a locomotive at night?
Answer. As soon as it begins to grow dark, the
head-light must be lighted and properly trimmed, and
the proper lamp signals placed in front of the engine,
if the rules of the road require the display of such
signals. A lamp should always be placed in the cab,
so as to throw its light on the steam-gauge, but not
into the runner’s face, because he is unable to see distant
signals so well if his eyes are exposed to the
glare of a light near him.
At night, as objects which are passed can not be
seen distinctly, it is more difficult to tell the speed at
which an engine is running than it is in the day time.
A runner should therefore consult his watch frequently,
and by counting the revolutions of the
wheels, which he can do by the sound of the pump
valve or other part of the machinery, he can tell from
the rule given in the answer to Question 438 the
speed at which the locomotive is running. From this
rule a table can easily be constructed for an engine
with any size of driving-wheels, showing the speed
for any given number of revolutions per minute. It
will be a good exercise for a young locomotive runner to
construct such a table, which will be found very convenient
for reference if placed in a conspicuous place
in the cab.
Question 488.What must be attended to in very cold
weather?
Answer. Great care must be exercised to prevent
the water in the pumps, pipes and in the tender from
freezing. If it does it will be almost certain to break
the pump or burst the pipes. To avoid this the
heater cocks must be opened so as to keep the water
in the tender warm. In excessively cold weather the
engine should be run with greater caution than at
other times, as iron is then more brittle, and also
more liable to break, owing to the frozen condition
and consequent solidity of the track.
Question 489.In running a locomotive in severe
snow or rain-storms, what should be observed?
Answer. Whenever it snows the pilot or cow catcher
should be covered with boards, or, better still, with
sheet iron, so as to act like a snow plow. Brooms
made of steel wire should be placed in front of the
front wheels of the engine, so as to sweep the snow
from the rails. The front damper on the ash-pan
should be kept closed so as to exclude the snow from
the ash-pan, which would soon fill it up, and in this
way obstruct the draft. If the fall of snow is very
heavy or it blows into drifts, the train must of necessity
run very slowly, and even if a part of the track
is clear of snow, it is unsafe to run fast on it, as there
would be danger of throwing the engine off the rails
if it should run into a heavy drift at a high speed.
In severe rain storms bridges, culverts and such
portions of the track as are liable to be washed away
should be approached cautiously, especially at night.
In both snow and rain-storms, and also in fogs, great
caution is required, owing to the difficulty of seeing
signals.
Question 490.What is meant by a reserve engine or
“helper?”
Answer. A reserve engine is a locomotive which is
not employed in hauling a regular train, but is kept
as a “reserve” to go to the help of an engine which
may be compelled to stop on account of an accident of
any kind, or to assist engines in moving trains up
heavy grades, or is used in clearing away a wrecked
train, rebuilding bridges or other structures.
Question 491.What must be observed in running a
reserve engine?
Answer. As no special arrangements are usually
made in preparing time-tables[110] for the running of reserve,
or as they are usually called by railroad men,
“wild” engines, it may very probably happen that it
will be called upon to assist other engines when the
road is not clear, and therefore its runner must constantly
be on the look-out for signals to stop, which
are often given suddenly. He must switch off with
special caution in order to be sure to keep out of the
way of regular trains running in the opposite direction
on the same track. When he reaches the train
or place where the assistance of the reserve engine is
needed, he must approach it slowly and carefully, in
order to avoid a violent shock. On the return from
the assisted train, he incurs the same danger, and
must pay close attention to any signal to stop made to
him by any opposite train on the same track, and also
on his part warn such trains by the proper signals.
[110] A time-table is a table which gives the time when each train shall
arrive at the stations it passes, the stations at which it shall stop, and
all the regulations by which it shall be run.
When a train is run with two engines, both in front
of it, the forward one always takes the management
of the train. The runner of the hind engine must be
guided by the signals of the runner of the forward engine.
In starting, the forward engine must be set in
motion first and then the one behind it. In stopping,
the steam must be shut off first in the hind engine.
Likewise in decreasing the speed during the trip, the
hind engine must first regulate the flow of steam. If
these precautions are not observed the forward engine
may easily be thrown from the track by the faster motion
of the hind one.
When a train is assisted by a “helper” placed behind
the train, and therefore pushing it, the forward
engine must likewise be set in motion first, and steam
should be let on in the hind engine only after a signal
has been given by the runner of the head engine.
During the run both engines must move with the
same speed.[111]
[111] Katechismus der Einrichtung und des Betriebes der Locomotive, by
Georg Kosak.
Question 492.How should switching engines be
managed?
Answer. In pushing and switching the freight cars
in the station-yard, they should be moved carefully
and severe shocks must be avoided, as the cars, the
goods with which they are loaded and the persons employed
about them may be injured by violent concussions.
The runner must also follow the instructions
of his superior strictly and cheerfully, and should examine
patiently and observe with discretion the suggestions
of employes who are not his superiors.
In this service it is also of special importance that
the runner give a distinct signal with the whistle or bell
before every movement of his engine, in order to warn
in time those who at such times often stand on the
track in the way of the engine or cars, or the persons
engaged in loading, cleaning or repairing the cars,
and thus give them time to get out of the way.[112]
Question 493.In firing a locomotive, what are the
most important ends to be attained?
Answer. That which is of first and chief importance
is to make steam enough, so that the locomotive
can pull its train and “make time”[113]; second, it must
make the requisite quantity of steam with the least
consumption of coal, and third, with the least production
of smoke, although the latter, independent of the
economy of combustion, is considered of importance
only with passenger trains. What is frequently lost
sight of in considering this subject is the fact that
with all locomotives it often happens that it is a matter
of extreme difficulty to make enough steam to do
the work required of the engines. When a freight
train is struggling up a grade with a heavy train, or
an express engine is obliged to make time under similar
conditions, it often depends entirely upon the
quantity of steam which can be generated in the
boiler in a given time whether the engine will fail or
not. In firing, therefore, the most important end to
be aimed at is often simply to produce the largest
amount of steam possible in a given time, even at the
sacrifice of economy or by producing any quantity of
smoke. Any means of economizing fuel or of smoke
prevention, which reduces the steam-producing capacity
of boilers, is therefore quite sure to be abandoned
in time.
[113] The term make time means to run at the speed indicated on the time-table.
Question 494.How can a boiler be made to produce
the largest quantity of steam in a given time?
Answer. By burning the greatest quantity of fuel
possible on the grate in that time. This can be done
by keeping the grates free from clinkers and the ash-pan
from ashes, and then distributing the coal evenly
over the grates in a layer six to twelve inches thick.
The thickness of the layer which will give the best
results will, however, vary with the quality of the
fuel, and must be determined by experience. If the
layer is too thick, not enough air will pass through it
to burn the coal. If it is too thin, then so much air
will pass through that the temperature in the fire will
be reduced. The rapidity of combustion will also be
promoted by breaking up the coal into lumps the size
of a man’s fist or smaller. If fine coal is used it
should be wet, otherwise it will be carried into the
flues by the blast before it is burned or caked or even
reaches the grate. Experience will indicate the
amount of air which can advantageously be admitted
above the fire in order to secure the maximum production
of steam. The best size of the exhaust nozzles
and the position of the petticoat pipe must also
be determined by experience. It will usually be
found, however, that if enough air is admitted above
the fire to prevent smoke, it will reduce the maximum
amount of steam which can be generated in a given
time. The fire should also be fed regularly and with
comparatively small quantities of fuel at a time, although
if the feeding is too frequent there is more
loss from the cooling effect which results from the
frequent opening of the furnace door than is gained
from the regularity of the firing. In this, too, a fireman
must consult experience to guide him.
Question 495.How can a locomotive be fired with
the least consumption of coal?
Answer. Two systems of firing are practiced in this
country, one known as the “banking system” and
the other the “spreading system.” When the banking
system is employed, the coal is piled up at the
back part of the fire-box, as shown in fig. 218, and
slopes down towards the front of the grate, where the
layer of coal is comparatively thin and in an active
state of incandescence. The heap of coal behind is
gradually coked by the heat in the fire-box and the
gases are thus expelled. Openings in the furnace
door admit air which mingles with the escaping gases,
which then pass over the bright fire in front, and are
thus supposed to be consumed. When the “bank”
of coal behind becomes thoroughly coked, it is pushed
forward on the bright fire and fresh coal is again put
on behind to be coked. This system of firing is practiced
on some roads with good results, but it is doubtful
whether it could be used successfully with coal
which cakes and clinkers badly.
The spreading system is most commonly employed
in the Western States, where the coal contains a
great deal of clinker. When this is practiced, the
coal is spread evenly over the whole of the grate in a
thin layer, and its success and economy depend upon
the regularity and evenness with which this layer of
coal is maintained and the fire fed. The thickness of
the coal must be adapted to the working of the engine.
When it is working lightly, the layer of coal should
be thin, but when the engine is pulling hard the layer
of coal must be thicker, otherwise the violent
blast may lift the coal off the grates. The success
of this system, as was explained in answer
to Question 388, depends upon the manner in
which the thickness of the fire is regulated, on the
admission of the proper amount of air above the fire,
and on the frequency with which the fire is supplied
with coal. When this system of firing is employed not
more than two shovels-full of coal should be put into
the fire-box at once, and if the engine is not working
hard, one or even less will be sufficient. The firemen
must, however, determine by experience the thickness
of fire, amount of air which should be admitted and the
frequency of firing which will give the best results in
practice. Doubtless these will vary with different kinds
of fuel and the construction of engines. Usually the
greatest obstacle in the way of producing good results
is the fact that firemen would rather “take things
easy” than exercise that diligence and observation
which will alone insure success in any occupation.
Question 496.How can smoke be most effectually
prevented?
Answer. The means of preventing smoke were very
fully explained in answer to Questions 379 and 388.
It may be said briefly that this can be done only by
properly regulating the supply of air which is admitted
to the fire. The means of doing this have already
been explained.
Question 497.What method of firing is employed
when anthracite coal is used?
Answer. The spreading system alone is then used.
Question 498.How may the rules which firemen
should observe when bituminous coal is used be briefly
stated?
Answer. 1. Keep the grate, ash-pan and tubes
clean. 2. Break the coal into small lumps. 3. Fire
often and in small quantities. 4. Keep the furnace
door open as little as possible. 5. Consult the steam
gauge frequently, and maintain a uniform steam pressure,
and if necessary to reduce the pressure do it by
closing the ash-pan dampers rather than by opening
the furnace door.
Question 499.On arriving at a station where a
train stops longer than a few minutes, what should the
locomotive runner and fireman attend to?
Answer. The runner should examine thoroughly all
the parts of his engine, as has been heretofore explained.
He should especially examine all the journals
and wearing surfaces to see whether they are hot.
This he can discover by feeling them. If any of them
have become very much heated, they must be cooled
by throwing cold water on them, and then thoroughly
oiled. In oiling a hot journal mineral oil should
never be used, as it is easily evaporated by the heat
and then takes fire. Animal oil should therefore always
be used on a hot bearing. The working parts
should be thoroughly lubricated, as already explained.
The fireman should examine the tank and see
whether it is necessary to take in a fresh supply of
water. He should then examine the grates and ash-pan,
and clean the cinders and clinkers from the former,
and the ashes from the latter. Neglecting to
clean the ash-pan may result in melting and destroying
the grate-bars, and by obstructing the admission
of air to the grates the ashes prevent the combustion
from being as complete as it would be otherwise.
With some kinds of fuel it is necessary to clean the
tubes frequently, which must often be done at stations
where the train stops.
During the stop, as thorough an inspection of the
engine should be made by the runner and fireman as
the time will permit; but any unnecessary waste of
time must be avoided, and the firing should be so managed
that nothing need be done about it during the halt
at the station. On starting again the same precautions
should be exercised as on making the first start.
Question 500.After reaching the end of its run, how
should an engine be cleaned and repaired?
Answer. Before reaching the last station the firing
should be so managed that there will be as little fire
as possible remaining in the fire-box at the end of the
run. After the arrival the engine should be run over
a pit which is usually provided for the purpose, and
the fire should be raked out of the fire-box by dropping
the drop-door if there is one to the grate, or
turning the grate-bars edgewise, or withdrawing one
or more of them if it is necessary to do so. In this
way the fire will fall into the ash-pan, from which it
can easily be raked. After all the fire is withdrawn
the dampers and furnace door should be closed so as
not to allow the cold air to cool the fire-box and tubes
too rapidly.
In order to keep the boiler clean, that is as free as
possible from sand, sediment or incrustation, it is necessary
to blow it out frequently if the water which is
used contains much solid or incrustating matter.
With “bad water” the boiler should be blown out as
often as possible. On some roads this is done after
each trip. In blowing a boiler out, the blow-off cocks
must be left open, and after all the water has escaped
the engine should be left to stand until it is cooled off.
If there is any considerable accumulation of mud or
sediment the hand-holes at the bottom of the fire-box
and the cover to the mud-drum should be taken off,
and as much of the mud removed as can be scraped out
through those apertures. A hose pipe attached to the
hose of a force pump should then be inserted through
these same openings, and a strong stream of water
forced into the boiler. By this means much of the
loose mud and scale will be washed out. The oftener
this is repeated of course the cleaner can a boiler be
kept. If a large amount of incrustation or mud has
accumulated about the tubes, some or all of them
must be taken out, so as to be able to remove the dirt.
After an engine is blown out, under no circumstances
excepting absolute necessity should it be filled
with cold water until it is entirely cooled off. It
should be remembered that any sudden change of temperature
in a boiler subjects it to very great strains
and incurs the danger of cracking the fire-box plates,
or causing the tubes to leak.
The tender should also be cleaned of the mud which
settles in it from time to time, but it is not necessary
to do this as often as it is to clean the boiler. All the
plates and flues should have the soot which sticks to
them thoroughly cleaned off.
Although the cleaning of the boiler and the grates
is usually committed to a special set of men, yet the
locomotive runner should examine them personally to
see that it is properly done. He should pay attention to
the condition of the grate, and see whether it is level and
smooth. As soon as one or more of the bars are bent
crooked, they usually burn out. If one of the bars is
burnt out the fire falls through the hole that it leaves
into the ash-pan, and then the fire under the grate
will heat it red hot, and finally may melt every bar.
Every grate-bar which is only a little damaged or bent
must therefore be removed as quickly as possible and
replaced with a new one.
As soon as the engine is run into the engine-house,
all superfluous grease which has escaped from the
wearing surfaces and the dust or mud which adheres
to the engine should be wiped off with cotton waste or
rags. This is usually done by men employed for the
purpose. While they are doing this, they should examine
every part thoroughly and observe whether it
is in good condition, and if any defects are found they
should be reported to the proper person whose business
it is to have them repaired. As the faithfulness
and skill of a fireman are often estimated by the good
or bad condition of his engine, he should, if for no
other reason, take pains to keep it clean and everything
in as good condition as possible.
If the engine is taken to pieces in order to be thoroughly
repaired, the runner, if he does not help to do
this, should watch carefully the taking it apart and
the putting it together again, as in this way he can
become thoroughly familiar with the construction of
the machine he runs.
Question 501.What precaution must be taken to prevent
the water in a locomotive from freezing, if it is laid
up?
Answer. In very cold weather, if engines are laid
up for any considerable time, no water must be left in
the tender, boiler or any of the pipes. If, however,
the engine must be soon used, and it is impracticable
to let the water out of the boiler and tender, then, if
exposed to the cold, a light fire must be kept in the
boiler sufficient to make steam enough to warm the
water in the tender. The water should, however, be
drawn out of the pumps and the feed and supply
pipes. This can be done by opening the pet-cocks,
and closing the tender valves and uncoupling the hose,
which will allow the water in the supply pipes to run
out. By running the engine a few revolutions the
pumps will then be emptied. The pipes and the
pumps can also be prevented from freezing without
uncoupling the hose if the tender valves are closed and
the pet-cocks opened, and steam is then admitted into
the supply pipes by the heater-cocks. This forces
part of the water which is in the pumps out of the pet-cocks
and warms the rest. This, however, requires
constant watchfulness to prevent freezing, and in excessively
cold weather, if the engine must lay up for
any considerable time, it is always best to empty the
pumps and pipes.
PART XXVIII. ACCIDENTS TO LOCOMOTIVES.
Question 502.What are the most serious accidents
which may happen in running a locomotive?
Answer. The most serious accidents are:
1. Collision of two trains approaching each other.
2. Collision of a moving with a standing train.
3. Collision of trains at the crossing of two railroads.
4. Running a train into the opening left by an open
draw-bridge.
5. Escape of an engine without any one on it.
6. Running off the track.
7. Explosion of the boiler.
8. Bursting or rather collapse of a flue.
9. Blowing out of a bolt, stud or rivet from the
boiler.
10. Failure of the feed-pumps, injector or check-valve.
11. Breaking or bursting of a cylinder, cylinder-head,
steam-chest, or steam-pipe.
12. Breaking or getting loose of the piston or cross-head
or bending of the piston-rod.
13. Breaking or bending of a connecting-rod or
crank-pin.
14. Breaking of a tire, wheel or axle.
15. Breaking of a spring, spring-hanger or equalizer.
16. Breaking of a frame.
17. Breaking or getting loose of a part of the valve-gear.
18. Failure of the throttle-valve.
19. Breaking of a coupling.
Question 503.What should be done to prevent a collision
when two trains are approaching each other?
Answer. The obvious thing to do is to stop the trains
as soon as possible. This is done by applying the brakes
at once with all their power, and then reversing the
engine, although it is best not to do the latter until the
train is somewhat checked, as there is always danger
of bursting the cylinder or breaking the cylinder-heads,
piston or connections if an engine is reversed suddenly
at a high speed. Of course the higher the speed,
the greater is the danger of injury from this cause,
and therefore it is best, if there is time, first to check
the speed of the train before reversing the engine.
When the engine is reversed, the sand-valves should
be opened so as to increase the adhesion of the wheels,
so that when their motion is reversed they may check
the speed of the train as soon as possible. On perceiving
danger ahead the order of procedure should be
as follows:
1. Shut the throttle-valve.
2. If the train is equipped with hand brakes alone,
blow the danger signal for their application, or if the
train has a continuous brake, apply it with its full
force.
3. Reverse the engine and open the throttle and the
sand valves.
4. If a collision is inevitable, shut the throttle-valve
before the engines meet, because if it is left open, after
the collision and when the speed of the train is checked,
the engine, if not disabled, will by its own power crush
through the wreck and thus do additional damage.
Question 504.What should be done if a standing
train should see another train approach it and there
should be danger of a collision?
Answer. The locomotive runner of the standing
train should start his engine in the same direction as
the approaching train is running, as quickly as possible,
because the shock of the collision will be very
much lessened if both trains are moving in the same
direction compared with what it would be if one was
standing still.
Question 505.What should be done to avoid a collision
at a railroad crossing?
Answer. As was explained in answer to Question
485, trains should always come to a dead stop before
crossing another railroad on the same level. If, however,
through any means danger of such a collision
should be incurred, then evidently the one train
should be stopped and the other moved out of the
way as soon as possible.
Question 506.How can an accident by running into
the opening at a draw-bridge be avoided?
Answer. First by ALWAYS coming to a dead stop
before reaching it, and second by not starting again
until it is absolutely certain that the draw is closed.
Of course if a locomotive runner of an approaching
train finds a draw open, the only thing he can do is
to stop as soon as possible.
Question 507.What measures should be taken to
prevent locomotives from escaping without a responsible
person on them?
Answer. In the first place when a locomotive is left
standing the throttle-valve should always be closed and
fastened, the cylinder cocks should also be opened so
that if any steam leaks into the cylinders it will not
accumulate there, but will escape, and the reverse
lever should be placed in the centre of the sector, so
that if by any accident the throttle should be opened
the engine will not start.
Question 508.If a locomotive should escape, what
should be done, and how may it be captured?
Answer. The first thing to be done is to telegraph
to the stations towards which the escaped engine is
running, either to keep the track clear, or, if there is
a train approaching, to open a switch and thus let the
engine run off the track. An escaped engine may be
captured by a swifter engine following it, but this is
always attended with great danger, as the first engine
may leave the track or become wrecked. A safer plan is
to telegraph ahead of the escaped engine and have
an engine placed in a position where the track can be
seen for a long distance in the direction in which the
runaway is expected. As soon as the latter comes in
sight, the waiting engine should start in the same direction,
so that when they get near to each other they
will both be running in the same direction and at
nearly the same speed. By regulating the speed of
the front engine, the following one may be allowed to
come up to it quite gently, and then a man can easily
climb from the one engine to the other, and thus both
be stopped.
Question 509.What should be done in case an engine
gets off the track?
Answer. The first thing to do is to close the throttle-valve
and “signal for brakes,”[114] or apply the continuous
brakes if the train is equipped with them,
and then reverse the engine. If its position after it
stops is much inclined, it is generally necessary to
draw the fire to prevent injury to the heating-surface,
a part of which is then usually exposed to the steam,
and therefore not covered with water.
[114] This expression means, among railroad men, to signal to brakemen
by blowing the whistle to have them apply the brakes.
Question 510.How is a locomotive replaced on the
track in case it gets off?
Answer. It is impossible to give any directions for
replacing locomotives on the track which will meet
the great variety of circumstances which occur in
practice. If the engine has not run far from the rails, it
can usually be run on again by placing blocks of wood
under the wheels and thus running them up to their
proper position, but if the engine falls on its side or
runs down an embankment, it is usually necessary to
send for the appliances which are now provided on
nearly all roads for removing wrecks and replacing
engines on the track. These appliances are generally
stored in what is called a wrecking or tool car, which
is placed at a convenient point on the road, from
which it can be sent to any place where its services
are likely to be needed. Such cars are generally provided
with ropes, jack-screws, chains, crowbars, levers,
etc., to be used in such cases, and generally a special
set of men is sent with the wrecking car to direct and
assist in replacing engines and cars on the track. It
would lead us too far to describe all the methods of
doing this employed under various circumstances; and
as such work seldom forms part of the duties of a locomotive
runner, a complete description would be out
of place here.
Question 511.After an accident which disables the
engine, what is the first thing to do?
Answer. The first thing to do is always to “protect
the train;” that is, to send out signal men in each direction
to stop approaching trains; otherwise they
might run into the wrecked train, and thus cause a
double accident.
Question 512.What is the chief cause of boiler explosions?
Answer. The cause of all boiler explosions, as happily
expressed by a prominent American engineer,[115]
is THAT THE PRESSURE INSIDE THE BOILER IS
GREATER THAN THE STRENGTH OF THE MATERIAL
OUTSIDE TO RESIST THAT PRESSURE. This may occur
in two ways: first, and most frequently with locomotives,
from insufficient strength of the boiler to bear
the ordinary working pressure; and second, from the
gradual increase of heat and pressure until the latter
is greater than the boiler was calculated to bear.
[115] See Fifth Annual Report of the American Master Mechanics’ Association,
page 196.
Insufficient strength may be due: 1, to defects of
the original design, owing to the ignorance of the
strains to which the material of the boiler will be exposed,
and its power of resistance; 2, to defective
workmanship and material, which can usually be discovered
by careful inspection; 3, to the reduction of
the original strength of the boiler by ordinary wear
and tear or neglect, which can also usually be discovered
by careful inspection.
The first two causes have been fully discussed in
the part relating to boiler construction, and the last
under the head of inspection of locomotives.
Over-pressure is nearly always due to some defect
of the safety-valve, or to the fact that it is overloaded.
This latter often occurs when safety-valves are set by
a defective steam gauge, which indicates too little
pressure. Over-pressure may also occur by letting an
engine stand alone with a large fire in its fire-box and
possibly with the blower turned on.
A boiler may, by suddenly opening the throttle-valve,
undoubtedly be subjected to very severe strain
that may possibly be sufficient to cause its destruction,
even though it had sufficient strength to bear the ordinary
pressure at which the safety-valve blows off.
Suddenly opening or closing the throttle-valve may
produce a violent rush of steam and water against the
part of the boiler whence the steam is drawn. The
percussion of the water and steam in such cases has
been known to shake the whole boiler, and to lift the
safety-valve momentarily right off its seat.[116] The
weakest parts of a locomotive are the two sides where
the barrel joins the outside fire-box. Many boilers,
especially those with a high wagon-top, have flat
spaces at this point, which it is impossible to stay
properly. It is at this point, too, that the expansion
and contraction of the tubes and the outside shell
exert their greatest strains, and it will therefore be
found, generally, that the seams at this point begin
to leak before any others, and for these reasons it is
believed that all the seams which join the outside
shell of the fire-box to the barrel should be double-riveted.
The practice of ascribing steam-boiler explosions to
obscure causes has been productive of much mischief,
as it engenders a carelessness on the part of those
having charge of them, who have been led to believe
that no amount of care will avail against the mysterious
agents at work within the boiler. Explosions
are also, in the absence of other convenient reasons,
very generally attributed to shortness of water. This
is often nothing more than a convenient method of
shifting the responsibility from the builder or owner
of the locomotive to the runner or fireman, who, if
not killed by the explosion, in many cases might just
as well be, so far as his ability to defend himself is
concerned.[117]
Question 513.What should a locomotive runner and
fireman do to avoid and prevent explosions?
Answer. 1. The height of the water in the boiler
should always be maintained so as to cover the heating
surfaces. 2. The boiler should be kept as clean,
that is, as free from scale, mud and other impurities,
as possible. 3. It should never be subjected to strains
from sudden heating or cooling. 4. The steam-gauge
and safety-valves should be examined and tested frequently,
to be sure they are in order; and 5, they
should examine every part of the boiler which is accessible,
but especially the stay-bolts, to see that
there is no fracture of any part or any injurious corrosion
or other dangerous defect.
Question 514.What should be done in case of the
bursting or collapse of a tube?
Answer. As soon as possible after it occurs, the
runner must stop the train, and close first the end of
the flue in the fire-box, and then that in the smoke-box,
by driving in iron plugs, which are usually provided
for the purpose. These plugs are attached to
the end of a bar, with which they are inserted into
the tubes. If the escape of water and steam from the
tube is so great as to make it difficult to see the end
of the tube, the steam may sometimes be drawn up
the chimney by starting the blower. If, however,
the escape is so great as to make it impossible to insert
the plug, then the steam pressure must be reduced
by running with both pumps on, or by starting
the injector; or it may be necessary to draw the fire
and cool off the engine. When a flue collapses, the
front end of which is behind the steam or petticoat
pipes, it is usually necessary to cool off the engine
before a plug can be inserted, especially if any considerable
amount of water and steam escape from it.
While driving in the plug, the runner and fireman
should always keep themselves in such positions that
the plug can not hit them in case it is blown out by
the steam. If the engine is not supplied with iron
flue-plugs, a wooden plug can be cut of the proper
size and driven in. This can be attached to the bar
referred to and inserted; but if no such bar is carried
with the engine, the wooden plug can be made on the
end of a long pole and then cut nearly off. It is then
inserted into the flue and driven in and broken off.
It will be found that such plugs will burn off even
with the end of the flue, but will not burn entirely
out.
Question 515.What should be done in case a bolt,
stud or rivet blows out of the boiler and thus allows the
steam or hot water to escape?
Answer. If it is accessible, cut a plug on the end of
a long pole and drive it in in the same way as described
above. This will avoid the necessity of cooling off
the engine; but in some cases it will be found that a
plug can not be inserted or driven in without drawing
the fire and cooling off the boiler.
Question 516.In case it is found necessary to draw
the fire and cool off the boiler, and if so much water
has escaped as to uncover the crown plate, what must be
done?
Answer. If the leak has been stopped or the fault
remedied, one of the safety-valves should be taken off
and water poured into the boiler with pails or buckets
through the opening left by the removal of the safety-valve
until the crown sheet is covered. The fire may
then be kindled again and the engine complete its
journey. When bituminous coal is used for fuel, the
necessity for drawing the fire in case of accident may
often be avoided by completely covering or “banking”
the fire with fine coal which has been wet, and
closing the dampers and opening the furnace door.
In this way the fire may be smothered and the boiler
cooled without putting the fire out, so that after the
defect is remedied it will not be necessary to rekindle
it.
Question 517.What must be done in case of the
failure of one or both of the feed pumps or of the injector
or check-valve?
Answer. If one of the pumps fails the other one
may be used, but the defect or obstruction to the first
should be remedied as soon as possible, because the
second may also fail. It will then be necessary to depend
upon the injector alone, if there is one, for feeding
the boiler. Only after all the appliances for
feeding the boiler have failed and the water is so low
as to be in danger of exposing the crown sheet, should
the fire be drawn or banked, and the runner should
then at once give the proper signals for warning and
the protection of his train, and if he is unable to repair
the pumps or injector, he must send for aid to the
nearest accessible point.
Question 518.In case a pump fails, how should it
be examined in order to discover the defect?
Answer. As explained in the answer to Question 458,
the working of a pump is usually indicated by the
stream which escapes from the pet-cock. If, when
this is opened, steam and water escape, it is an indication
that the check-valve is not working properly.
When this occurs hot water will escape if the pet-cock
is opened when the engine is standing still, but
the pump may still feed the boiler if the upper or
pressure-valve works properly. When the check-valve
does not work as it should, it is also indicated by the
heating of the feed-pipe, owing to the escape of hot
water from the boiler through the check-valve when
the pet-cock is opened. If, when the plunger is
drawn out of the pump, air is sucked in through the
open pet-cock, then the upper or pressure-valve of the
pump does not work, but the working of the pump
may still be secured by the working of the check-valve;
but if the pump, air-chamber and feed-pipe
then get filled with air, the plunger may compress
this air at each stroke, and as it can then follow the
plunger during its outward stroke, the latter will not
suck water, but will simply compress the air during
the inward stroke, which will then expand during the
outward stroke. This will be indicated by the escape
of air from the pet-cock when the plunger is moving inward,
and the suction of air when the plunger is moving
outward. This can be known by holding the hand
in front of the pet-cock. Usually, however, the air is
mixed with water so that the stream which escapes
from the pet-cock is broken or irregular. If air escapes
from the pet-cock during the inward stroke of
the plunger, but none is sucked in during the outward
stroke, it shows that there is a leak somewhere in the
pump or pipes, and that it is pumping air instead of
water. The leak may be in the stuffing-box of the
plunger, the joints of the pump or pipes, in the hose
or their connections with the supply-pipe or tender.
If neither air nor water escapes from the pet-cock
during the inward stroke of the pump plunger, or, if
the stream of water at that time is weak, then it indicates
that the suction or lower valve of the pump is
not working properly. The same thing will occur if
the pipe, pump or tender-valve is obstructed. If there
is a cock, as there always should be, just above the suction-valve,
it will aid us very much to discover the
fault when the pump will not work. If, when this
cock is opened, cold water escapes from it, the fault
is in the suction-valve; if hot water, then it is the
pressure and check-valves which are leaky, obstructed
or broken, and consequently the hot water from the
boiler leaks back into the pump. In the absence of
such a cock, the fault can often be discovered by feeling
the pump barrel with the hand. If the pump can
not be made to work, and the fault is found to be in
the lower valve, it must be taken out and examined; or
if the fault is in the pipes, it can usually be easily
remedied. If the pipes are burst with only a small
fracture, it can usually be remedied by covering the
aperture with canvas or rubber and wrapping twine
around it tightly. The upper valve of a pump must,
however, never be taken down without first being sure
that the check-valve is tight, because if it is not, the
person will be likely to be scalded in taking the pump
apart.
Directions for managing an injector, and also for
taking care of pumps in cold weather, have already
been given in the answers to Questions 142 and 488.
Question 519.What should be done in case of the
breaking or bursting of a cylinder or cylinder-head?
Answer. The main connecting rod must be taken
down on that side of the engine. The piston should
then be moved to the front or back end of the cylinder
and wooden blocks be placed between the guides so as
to fill up the space between the cross-head and the
end of the guide-bars, and thus prevent the cross-head
and piston from moving. The valve stem should then
be disconnected from the rocker, and the valve moved
to the middle of the valve face, so as to cover up both
steam-ports. It must then be fastened in that position
by screwing up one of the bolts of the stuffing-box
of the valve stem, so as to make the gland bind
against the valve stem. The train should then be run
cautiously to the next station with the use of one cylinder.
If the engine is not able to haul the train
with one cylinder, then it should be uncoupled from
the train and run to the first telegraph station or
other point where the aid of a helping engine can be
obtained or telegraphed for. In the meanwhile the
train must be protected by the proper signals. Should
the engine continue its journey with one cylinder, it
must be started, if it should happen to be standing at
the dead point, by pushing or by means of crow-bars.
In so doing, however, the bars should not be put between
the spokes of the wheels, as they may easily be
caught in the wheels when the engine starts, and in
this way the spokes be broken or the persons who are
using the crow-bars be badly hurt.
Question 520.What must be done in case a steam-chest
or steam-pipe is broken?
Answer. If a steam-chest is broken a block of wood
should be bolted over the mouth of the steam passage,
so as to prevent the escape of the steam from the
steam-pipe on that side. It will sometimes require
considerable ingenuity to devise means of fastening
such a block or blocks of wood so as to cover the
mouth of the steam passage. As cylinders are now
usually made, the blocks can be fastened by cutting
them to the proper form and size, and then placing a
thick block on top, and bolting the steam-chest cover
down on top of it. If the cover is broken, a part of
it may be used or a piece of plank with a few holes
bored into it be employed instead. In some cases a
piece of board can be bolted over the end of the steam-pipe.
When the latter is broken, it should be taken
down and a piece of board or plank bolted over the
opening of the ⊤-pipe to which the steam-pipe was attached.
The engine can then be run with one cylinder
as before, although usually in such cases it is not
necessary to disconnect any other parts than the valve
stem.
Question 521.What must be done if a piston, cross-head,
connecting-rod or crank-pin is broken or bent?
Answer. If the piston, cross-head or main connecting-rod
is broken, the same course must be pursued as
when a cylinder is broken. If a coupling-rod or a
crank-pin of a trailing-wheel is broken, then it is
necessary to take down both the coupling-rods, but not
to disconnect the main connecting-rods or their attachments,
unless they are injured.
Question 522.If one coupling-rod is broken or taken
down, why must the other be taken down also?
Answer. Because if only one rod is used there is then
nothing to help the cranks of the trailing wheels past
the dead-points, so that in starting, or if they are
moving slowly when they reach these points, they are
quite as likely to revolve in one direction as the other.
If they happen to turn in the reverse direction to that
in which the wheels to which they are coupled are
moving, then the crank-pins of one or the other pair
of wheels are very liable to be broken or bent.
Question 523.What must be done if a driving-wheel
tire or driving-axle breaks?
Answer. If a tire on a main driving-wheel or the
wheel itself breaks, the driving-box of the broken
wheel or tire should be held up by putting a wooden
block under the box. An ordinary American engine
can then be run on three driving-wheels, but it must
be run with the utmost caution. If the engine has
more than four driving-wheels there is usually less difficulty
in running it, if one of the main wheels is injured,
than if there are only four. But it is almost
impossible to give directions which will be applicable to
all the accidents of this kind that may occur to different
kinds of engines. If none of the connecting-rods,
crank-pins or crank-pin bosses are injured, it is not
necessary to disconnect either side, but if the injury
is of such a nature that the coupling-rod must be
taken down on one side, the one on the other side
must be taken down too. If the main crank-pin and
connecting-rod are not disabled, both cylinders may be
used even if one of the main wheels or tires is broken.
But even if one side of the engine must be entirely
disconnected, the engine may still be run with one
cylinder and by driving one wheel. If a main axle
breaks the engine can usually be run, but great caution
must be exercised. In such cases, however, if
assistance or a telegraph office is near where the accident
occurs, it is usually best to send for assistance at
once, rather than take the risks which attend the attempt
to run an engine so seriously injured.
Question 524.What must be done when a trailing or
leading driving-wheel, tire or axle breaks?
Answer. Very much the same course must be pursued
as was described in the previous answer, although
it is generally less difficult to run with a trailing or
leading axle broken than it is when the main axle has
met with such an accident.
Question 525.What must be done if an engine-truck
wheel or axle breaks?
Answer. It is usually best to chain up the end of the
truck-frame over the broken axle or wheel to the engine
frame and place a cross-tie across the other end
of the truck-frame, between it and the engine frame,
so that the weight of the engine may rest on the cross-tie.
If a part of the flange or a piece of the wheel is
broken out, the wheels should be turned around so that
the unbroken part will rest on the rail, and they
should then be chained or otherwise fastened so that
they cannot revolve, and thus be made to slide on the
rails and carry the weight of the engine in that way.
The same plan is employed if a tender wheel breaks,
but one end of a tender-truck frame must be chained
up. It is usually necessary to place a cross-tie across
the top of the tender, and fasten the chains to it.
Question 526.What must be done in case a driving-spring,
spring-hanger or equalizing-lever breaks?
Answer. As the breaking of a spring or spring-hanger
may cause a more serious accident, the engine
and train should be stopped as soon as possible after
it occurs. If the hanger is broken and there is a duplicate
on hand, it should be substituted in place of
the broken one. If there is no duplicate, then the
spring should be taken down, and a wooden block
be placed between the top of the driving-box and
the frame to support the weight which before rested
on the spring. In order to insert this block, if it
is a front spring which is broken, it is usually best
to raise the engine with jack-screws or run the back
wheels on inclined blocks of wood placed under each
of the back wheels. This raises the weight off from
the front-wheels, and the block can then be inserted between
the box and frame. If it is one of the springs over
the back wheels which is broken, the front wheels should
be run on the wooden wedges. Such wedges can soon
be cut out of a cross-tie with an axe, or by sawing a
square stick of wood diagonally it will make two such
wedges. The end of the equalizing lever next to the
broken spring must be supported by inserting a piece
of wood under it. This will usually be held securely
by the weight which is suspended from the opposite
end, bearing the blocked end down on the block.
Question 527.What should be done if an engine-truck
or tender spring breaks?
Answer. Very much the same course must be pursued
that is employed when a driving-spring breaks,
excepting that usually the weight can be lifted off
from a truck-box easier by placing a jack under the
end of the truck-frame than by the method described.
Usually, too, each of the truck-springs supports the
weight on two of the wheels, so that the two boxes
must be blocked up.
Question 528.What must be done in case the engine-frame
is broken?
Answer. Usually very little need be done excepting
to exercise more than usual caution in running,
and to reduce the speed. Of course the breakage of a
frame may disable the engine, but ordinarily in such
accidents that is not the case.
Question 529.How can it be known if an eccentric
has slipped on the axle?
Answer. It is indicated at once by the irregular
sound of the exhaust, or, as locomotive runners say,
the engine will be “lame.”
Question 530.When it is known that an eccentric
has slipped, how can it be learned which is the one that is
misplaced?
Answer. This can usually be learned by examining
the marks which should always be made on the eccentrics
and on the axles. If no such marks have been
made by the builder of the engine, the runner himself
should make them, after the valves have been set correctly.
The effect upon the valve when an eccentric
slips is either to increase or diminish the lead. Therefore,
by running the engine slowly with the link first
in full forward and then in full back gear, and observing
whether steam is admitted at each end of the cylinder
just before the crank reaches the dead points, it
can be known which eccentric has moved. If it has
slipped in one direction the lead will be increased and
steam will be admitted to the cylinder some time before
the piston reaches the end of the stroke. If it
has moved the opposite way, the lead will be diminished
and steam will not be admitted until after the
piston has reached the end of its stroke. The admission
of steam will be indicated by its escape from the
cylinder cocks.
Question 531.If by any means the valve stem or
either of the eccentric rods should be lengthened or shortened,
how can it be known?
Answer. The crank on one side should be placed
at one of the dead points and the cylinder-cocks
opened; then admit a little steam to the cylinder, by
opening the throttle-valve slightly, and throw the reverse
lever from full gear forward to full gear backward,
and observe whether steam escapes all the time
from the end of the cylinder at which the piston
stands. Then repeat the operation with the crank at
the other dead point. If either of the eccentric rods
or the valve stem have been lengthened or shortened,
it will cause the valve to cover the steam-port either
at the front or back end of the cylinder, so that no
steam will escape from the cock at that end. If the
length of one of the eccentric rods has been changed,
then when the altered rod is in gear the valve will
have too little or no lead at one end of the cylinder
and too much at the other. If, therefore, this occurs
when the forward rod is in gear and not in back gear,
it indicates that the length of the forward rod has
been altered. If the reverse occurs it shows that it is
the back-motion rod whose length has been changed.
It must be observed that if the length of an eccentric
rod is altered the lead will be changed only at that
part of the link which is operated by the altered rod.
That is, if the forward eccentric rod is too long or too
short, the lead at the front and back ends of the cylinder
in forward gear only will be affected. If the back
eccentric rod is changed the valve will be affected only
in back gear. If, however, the length of the valve
stem is changed, the lead will be changed in both
forward and back gear. The valves on each side of
the engine can, of course, be tested in the same way.
Question 532. When it is discovered which eccentric
has slipped, how should it be reset?
Answer. If it has been marked, it is simply turned
back so that the marks correspond with each other
again. This is done by first loosening the set-screws,
and, after the eccentric is turned to the proper place,
tightening them up again. When an eccentric slips
it is often caused by the cutting of the eccentric-straps,
valve or other part of the valve-gear, so that
these should always be examined to see whether they
are properly oiled. If the eccentrics have not been
marked, the valve may be set by placing the crank at
the forward dead-point, and the reverse lever in the
front notch of the sector and the full part of the
forward-motion eccentric above the axle. Then admit
a little steam into the steam-chest, open the cylinder
cocks, and move the forward-motion eccentric slowly
forward until steam escapes from the front cylinder
cock, which will show that the steam-port is opened
and the valve has some lead. To set the backward-motion
eccentric the crank is placed in the same position,
but the reverse lever is thrown into the back
notch and the full part of the eccentric is placed below
the axle. Then move this eccentric forward until steam
escapes from the front cylinder cock as before. In
order to verify the position of the eccentrics the
crank may be placed at the back dead-point and the
reverse lever moved backward and forward, at the
same time observing whether steam escapes from the
back cylinder cock when the link is in back and forward
gear.
Question 533.What should be done in case an eccentric-strap
or rod, or rocker arm or shaft, or the valve
stem breaks?
Answer. If an eccentric-strap or rod breaks, the
broken rod and strap should be taken down, and the
valve-stem disconnected from the rocker and the
valve fastened in the middle position of the valve
face, and the engine should be run with one cylinder
only. The same course must usually be pursued if a
rocker breaks. If the valve-stem breaks, it is not
necessary to disconnect the link and eccentric rods,
but simply to fasten the valve in the centre of the
valve face.
Question 534.If a link hanger or saddle, or a lifting
arm should break, what may be done?
Answer. The valve-gear may be used on that side
of the engine by putting a wooden block in the link
slot above the link block, so as to support the link
near the position at which it works the valve full
stroke forward. Of course the engine can then be
run in only one direction, and should therefore be
run with the utmost caution. If, however, it should
be necessary to back the train on a side track, it can
be done by taking out the wooden block and substituting
a longer one, so that the link will be supported
in a position near that at which it works the valve full
stroke backward. These blocks must be fastened in
some way, either with rope or twine, so that they will
be held in their position when the engine is at work.
Question 535.If the lifting shaft itself or its vertical
arm, the reverse lever or rod, should break, what can
be done?
Answer. If it is impossible to devise any temporary
substitute or method of mending them, both links can
be blocked up as described above.
Question 536.In case the throttle-valve should fail,
what should be done?
Answer. If such an accident occurs, especially if it
happens about a station, it is attended with great
danger. If it is found that steam can not be shut off
from the cylinders with the throttle-valve, then the
reverse lever should be placed in the middle of the
sector. If this does not prevent the engine from
moving, the reverse lever should be alternately
thrown into forward and then into back gear, and
at the same time every aperture, such as the safety-valve
and heater cocks, should be opened, and every
means be taken to cool the boiler as quickly as possible.
The fireman should open the furnace door, close
the ash-pan dampers, and start the blower so as to
draw a strong current of cold air into the furnace
and through the tubes. At the same time the injector
should be started and the fire drawn as quickly as
possible. After the boiler is cooled, the cover of the
steam-dome may be removed and the valve examined
if the defect can not be discovered in any other way.
Of course if the accident occurs on the open road, the
train must be at once protected by sending out signals
in each direction.
Question 537.What must be done in case a coupling
breaks?
Answer. When a coupling between the cars or tender
breaks, if the front end of the train is immediately
stopped, there will be danger that the back end
of it, which is broken loose, will run into the front
end, and thus do great damage. As it always occurs,
when a coupling of a passenger train breaks, that the
signal bell in the cab is rung, the first impulse of a
runner under such circumstances is to stop the engine.
He should, however, be careful not to do so if on shutting
off steam he finds that the train has broken in
two, but should at once open the throttle in order to
get the front end of the train out of the way of the
rear end. The ease with which the speed of a train
is arrested with continuous brakes has increased the
danger of accident from this cause. Usually a runner
learns by the sudden start of the engine that the train
has separated, and when that occurs he should never
apply the brakes.
Question 538.If from any cause the supply of
water in the tender becomes exhausted, what must be
done?
Answer. It is best, if it can be done without risk of
injury to the engine, to run the train on a side track
and then draw the fire. If no water can be obtained
near enough to supply the tender with buckets, help
must be sent for; but if there is a well, stream or
pond of water near, the tender can be partly filled
by carrying water.
Question 539.In case an engine becomes blockaded
in a snow storm with plenty of fuel, but runs out of
water, what can be done?
Answer. Snow should be shoveled into the tender
and steam admitted through the heater cocks so as to
melt the snow.
Question 540.If a locomotive without an injector
should be obstructed in a snow storm or in any other way
so that it could not move, and therefore could not work
the pumps, what should be done in case the water in the
boiler should get low?
Answer. The weight of the engine should be lifted
off from the main driving-wheels and the coupling
rods disconnected from the main crank-pin, so that
the main wheels can turn without moving the engine.
These can then be run and the pumps thus be worked.
The weight can usually be most conveniently taken
off from the main wheels by running the trailing
wheels on wooden blocks, and thus raising up the
back end of the engine.
Question 541.If it is impossible, in a snow storm
or in very cold weather, to keep steam in the boiler without
danger, what should be done?
Answer. Draw the fire, blow all the water out of the
boiler, empty the tanks, disconnect the hose and
slacken up the joints in the pumps and injector so
that all the water in them can escape, and thus prevent
them from freezing up.
PART XXIX. ACCIDENTS AND INJURIES TO PERSONS.
Question 542.In case an accident occurs and one
or more persons are seriously injured, what can be done
by those present?
Answer. In such cases it very often happens that
with knowledge and sufficient coolness to apply that
knowledge, one or more non-medical persons who are
present when an accident occurs can do as much or
more toward saving life and allaying pain, before a
doctor comes, than he can afterwards. The following
cases cited by Dr. Howe in his book on “Emergencies”
will illustrate this:
“Case 1.—A machinist was admitted to a New
York hospital suffering from wounds of the wrist and
palm of the hand. On arriving at the hospital the
entire clothing on one side of his body was saturated
with blood, from the loss of which he was partly insensible.
On making an examination, it was found
by the surgeon that a folded handkerchief was bandaged
over the centre of the wrist, and that the
wound in the palm of the hand was untouched. The
pad was placed on the wrist, as if the greatest care
had been exercised to avoid pressing on either of
the two arteries. The bleeding in this case could
easily have been controlled if the bandage and pad
had been properly applied. The patient, however,
developed erysipelas, and, not having sufficient vitality
to carry him through, died the fifth day.”
“Case 2.—A laborer fell from the front platform of
a car at Harlem, and had his right foot crushed by
one of the wheels. An ordinary bandage was placed
on the limb without any compress over the vessels.
In bringing the man to the hospital, the rough jolting
of the carriage set the wound bleeding, and by the
time he reached his destination he was apparently
lifeless. The vessels were tied and stimulants administered,
but he never rallied. Death occurred
six hours after his admission. His injuries, independent
of the bleeding, might indeed have terminated
his life; still the chances would have been in
his favor if a compress had been applied to the limb
to prevent bleeding. The fact that such a thing was
not done shows either culpable negligence or deplorable
ignorance.”
Many similar cases constantly occur where a little
intelligent timely action of those present would save
the life of an injured person, who without such help
must die before professional surgical aid can be obtained.
Question 543.When it is found that one or more
persons are seriously injured, what is the first thing to be
done?
Answer. The first thing to do is to extricate the
person or persons from the danger, and at the same
time send a messenger for a doctor. If it is doubtful
if one can be obtained by sending in one direction,
send two or more messengers in different directions.
Question 544.To what kind of injuries are locomotive
runners and other persons employed or traveling on
railroads exposed?
Answer. They are liable to be bruised or crushed in
case of collision or running off the track, or of injury
from falling off the train, or of being run over by a
moving train. Brakemen and others whose duty it is
to couple cars are liable to have their hands, arms or
bodies crushed between the cars, and locomotive runners
are sometimes burned or scalded if an accident
happens to their engines. Train-men are also frequently
exposed to very great cold in winter and heat
in summer, and are thus liable to be frost-bitten or
sun-struck. Passengers are seldom injured excepting
through their own carelessness, unless in cases of collision
or running off the track and the destruction of
the cars. Strangers and even railroad employes are
frequently run over by trains while walking on the
track, and frequent accidents occur to deaf people in
this way, and it is not very unusual to hear of train-men
who sit on the main track at night while their
trains are waiting on the side-track for another train
to pass, go to sleep while in that position, and then
are run over by the passing train.
Question 545.When persons are crushed or dangerously
wounded, what are the chief immediate sources of
danger and death when their wounds are not necessarily
fatal?
Answer. First, excessive bleeding in case an artery
is ruptured; second, the shock to the whole system,
from which the sufferer may not have the strength to
recover.
Question 546.When does bleeding from a wound become
dangerous?
Answer. Profuse bleeding is always dangerous, but
it should be remembered that bleeding occurs from
two sources: first from the arteries, which are the vessels
which convey the blood from the heart, and second
from the veins, through which the blood flows back to
the heart. The first is called arterial bleeding and the
second venous bleeding. Now it must be remembered
that the heart is the great force-pump of the body,
and that it supplies all parts of the body with blood,
somewhat as the feed-pump of a locomotive supplies
the boiler with water. The arteries referred to fulfill
the same purpose that the feed-pipe does to a locomotive
pump—they convey the fluid from the pump
to the place where it is needed. Now the blood is
forced into these arteries with a certain amount of
pressure, so that if any of them are cut or injured the
blood will flow out in a jet or spurt just as the water
will escape from a feed-pipe if that is ruptured. The
blood which flows through the veins back to the heart
may, on the other hand, be compared to the water in
the supply pipes of a locomotive pump, that is, there
is very little pressure on it, and therefore if they are
injured the flow of blood from them is less rapid than
from the arteries. It will therefore be seen that arterial
bleeding is much more dangerous, because the
blood flows from them under a pressure.
Question 547.How can arterial bleeding be distinguished
from venous bleeding?
Answer. The blood is of a bright scarlet color, and is
forced out in successive jets; each jet corresponds
with the movements of the heart. This characteristic
spurting is caused by the intermittent force-pump
action of the heart, driving out the blood. Venous
bleeding is distinguished from arterial by the dark-blue
color of the blood when flowing from the wound.
It never flows in repeated jets, but oozes slowly from
the wounded surfaces. Venous blood is traveling toward
the heart, and there is consequently little force
behind to cause a more rapid flow. This form of
bleeding is comparatively harmless, unless occurring
from very large veins.[118]
[118] “Emergencies and How to Treat Them,” by Joseph W. Howe,
M. D.
Question 548.How can the bleeding be stopped in
case an artery is cut or ruptured?
Answer. The most efficient and available method is
the application of PRESSURE on the artery BETWEEN
THE WOUND AND THE HEART. Under ordinary circumstances
this can be most effectively done with what
is called a field tourniquet, which is simply a handkerchief
passed around the limb above the wound, the
ends of which are then tied together. A pad is then
made, either of cloth rolled up, a piece of wood, or a
round stone about the size of a hen’s egg well wrapped,
or any substance from which a firm pad can be quickly
made, which is placed over the artery. The handkerchief
is then placed over the pad and a short stick
put through it on the opposite side of the limb and
twisted around until the pad compresses the artery
firmly. While the tourniquet is being prepared, some
one should compress the artery with his fingers or
thumb, so as to prevent as much loss of blood as possible.
Question 549.What is the position of the arteries in
the body and how can their location be known?
Fig. 230.
Answer. The position of the principal arteries is
shown in fig. 230. They proceed from the heart h
with branches, a, a, and b, b, which extend along each
limb. These branches subdivide again below the
knees and elbows, and again in the hands and feet.
The position of the arteries can be felt by their pulsation
at almost any part of them, but when they are
buried below the muscles it is more difficult than when
they are near the surface.
Question 550.In case of a wound and rupture of the
arteries in the arm, what should be done?
Answer. The artery at a should be firmly compressed
with the thumb until a bandage and pad from
which a tourniquet can be made are prepared. The
pad should then be applied over the artery and compressed
as explained in answer to Question 548. The
bleeding can also be stopped by placing a round piece
of wood or other form of pad between the arm at a
and the body and then tying the arm tightly against the
body, so that the pad will be pressed against the arm.
Question 551.In case of rupture to an artery below
the knee, where should the pressure be applied?
Answer. The artery approaches near the surface at
c, c, immediately back of the knee, where it is represented
in dotted lines in fig. 230. Pressure should therefore
be applied at that point first with the thumb until
a tourniquet can be applied. The bleeding can also be
stopped by elevating the leg and allowing it to rest
on the back of a chair or other similar support. The
weight of the leg will then bring sufficient pressure
on the artery to stop the bleeding. A towel or other
soft material should be placed over the back of the
chair, so that the pressure will not be too painful to
the sufferer.
Question 552.If an artery is ruptured in the leg
above the knee, where should the pressure be applied?
Answer. In the thigh at b, where the beating or
pulsations in the artery can be distinctly felt. The
reader should familiarize himself with the position of
the arteries by feeling their location in his own body.
By doing so he may be able to save the life of a companion
or other person in case of accident, whereas
without such knowledge the injured person would die.
Question 553.After the arterial bleeding has been
stopped, if blood should continue to ooze out of the wound,
what should be done?
Answer. The wound should be filled with lint or
cotton waste; and the limb then be bandaged by beginning
at its extremity and wrapping the bandage
closely and evenly around it so as to bring, as nearly
as possible, an equal pressure on the whole of it.
Bandaging the limb in this way up to the point
where the pressure is applied to the artery, will prevent
swelling, and the veins will be compressed so
that the blood will not flow from their torn extremities.
Question 554.When the bleeding has been stopped,
what should be done?
Answer. The injured person should be laid in as
comfortable a place as can be procured for him, and
should be given a moderate drink of water. If much
exhausted, two or three tablespoonsful of brandy or
whisky, mixed with an equal quantity of water,
should be given first, and smaller quantities, of notMORE THAN A TABLESPOONFUL at a time, should
then be given every half hour. Usually wounded
persons are given too much stimulant, so that frequently
they are injured more than they are benefited
thereby.
After a person has lost much blood, he feels an intolerable
thirst, but if too much water is given him,
he is apt to become sick and vomit, which weakens
him still more. It is therefore best to give him very
little water, say a teaspoonful at a time, after the first
drink, or if ice can be obtained, give the sufferer
pieces of ice frequently, which can be allowed to melt
slowly in his mouth.
Question 555.When a person is insensible, what
should be done for him?
Answer. Lay him down in as comfortable a place as
the circumstances will permit, and protect him from
cold, rain or hot sun, as may be needed. A common
error is to place injured and insensible persons in an
erect position or in a chair. If he is insensible he
should always be laid down with his head slightly
lower than his body. Then water should be dashed
two or three times on his face, and warm bricks, stones
or pieces of iron, such as coupling links or pins, applied
to his feet and in the arm-pits and between the
thighs, being careful that the warm objects applied
are not hot enough to burn. Then cover the person
with blankets, heavy coats or anything else which
will keep him warm. Wounded persons soon become
cold and chilled, the effects of which are very
injurious, and therefore especial pains should be taken
to keep them warm. In very cold weather there is
great danger that injured persons will be frost-bitten,
which must be carefully guarded against.
In case of shock, when the injured person lies pale,
faint, cold and sometimes insensible, with feeble
pulse and labored breathing, anything like excitement
must be avoided, as it tends to exhaust the patient.
All assistance and attention should be given to
a wounded person with the least noise and excitement,
and all crowds and idle spectators should be driven
away and every effort made to keep the sufferer comfortable
and quiet. If food is given it should be in
the form of beef tea or broth, and in small quantities
at a time.
Question 556.In case any bones are broken, what
should be done?
Answer. The limb should be supported as comfortably
as possible until a doctor’s services can be obtained.
There is danger with a broken limb that the
bones will protrude through the flesh and skin, to
avoid which the limb should be placed in a natural
position and laid on a pillow, car cushion or other soft
object. This should then be wrapped around the
limb and tied in this position, so as to prevent any
movement of the broken bones.
Question 557.If a person is crushed or severely
burned, what should be done?
Answer. The immediate danger from such injuries
arises from the “shock” to the system. It is usually
best to bandage the part which is crushed until surgical
aid can be obtained, and the sufferer treated as
explained in answer to Question 548.
Question 558.What should be done for a person
who has been burned or scalded?
Answer. Lint or cotton waste saturated with molasses
and water should be applied to the wound, or the
latter should be dusted with wheat flour, and then
dressed with lint or cotton waste, and loosely bandaged.
If the injury should be severe, a shivering followed by
depression is very likely to come on. To check this,
warmth in the form of hot applications and stimulants
should be used, as already explained.
Question 559.What should be done for a frost-bite?
Answer. Warmth should be applied to the frozen
part very gradually by rubbing with snow or pouring
cold water on it. The occurrence of stinging pain,
with a change in color, is a signal to stop all rubbing
or other measure which might excite inflammation.
If the frozen part turns black the next day, a poultice
should be applied.
If persons exposed to the cold become very much
exhausted or sleepy, stimulants should be given, as
explained in answer to Question 554, and the body
briskly rubbed with the hands and warm flannel or
other woolen material.
Question 560.How should a person be treated who
has been sun-struck?
Answer. Apply cold water or ice to the head, place
the sufferer in a cool place, and make him comfortable.
After being sun-struck the person should not
work for some days or weeks thereafter, until his
health and strength are fully recovered.
PART XL. RESPONSIBILITY AND QUALIFICATIONS OF LOCOMOTIVE RUNNERS. [119] — LIST OF BOOKS FOR MECHANICS, LOCOMOTIVE RUNNERS, FIREMEN, ETC.
[119]Note.—The
greater part of this chapter is a translation from Prof.
George Kosak’s “Katechismus der Einrichtung und des Betriebes der Locomotive.”
Question 561.What are the dangers to which the
runner and the fireman are exposed by their work on the
engine?
Answer. Runners and firemen are not only exposed
to great bodily injury or even death by every accident
which may happen to their engine, but unless they are
very careful to preserve their health it is quickly destroyed
by the constant changes of the weather to which
their position exposes them, and also by the effect of
the heat of the fire and by the smoke by which they
are often surrounded.
In order to protect themselves in a measure from
the injurious effects of change of weather, smoke, cold,
etc., frequent bathing and cleansing of the skin are absolutely
necessary, and also the wearing of a woolen
undershirt next the skin at all seasons.
The gases of coal which pour out of the furnace-door,
if it is opened when the throttle is closed, have
an especially injurious effect on the throat, lungs, etc.
They should always see to it, therefore, that the
blower is always started before the fire-door is opened,
in order that these injurious gases, which have collected
during a halt, may be drawn forward and up
the smoke-stack by the draft.
The steady, loud clatter which the engine makes
while running has an injurious influence on the nervous
system. The runner should therefore endeavor
to lessen these shocks of the engine as far as possible
by keeping watch over it and keeping its parts accurately
adjusted. In order to keep himself fresh and
strong in his service, which is extremely exhaustive
to body and mind, the runner must try to strengthen
himself by regular, temperate living, and eating abundant
nourishing food. The common use of strong
drinks, which undermines the mental and physical
strength of men, should be avoided by a person occupying
the exhaustive and responsible position of a
locomotive runner. If in ordinary life a drunken man
is unfit for any simple work, how shall a drunken runner
or fireman undertake the difficult management of
so great, so delicate and so costly a machine as a locomotive?
How can hundreds of men quietly trust
their lives and limbs to such a man, whom no one
can help despising? Rightfully, therefore, conscientious
railroad managers place the greatest stress on
the sobriety of the runners and firemen, and instantly
discharge from their service those who give themselves
up to a passion for drink.
Owing to the demands which their daily labor
makes upon their strength and endurance, locomotive
runners should be careful not to increase the drain by
dissipation, irregular hours or overwork. There seems
to be something about the power of endurance of the
human frame analogous to the capacity of a bar of iron
or steel to resist strains. So long as the strains do
not exceed the elastic limit, that is if the bar recovers
its original length when the strain is removed, it will
bear millions of such strains without becoming weaker;
but if it is strained so hard that it is permanently
stretched, then comparatively few applications of the
force will rupture the bar. In a similar way, if the
strain or fatigue which a man endures is no more than
he will recover from after the ordinary rest, he can
endure an almost unlimited number of such strains,
but if the fatigue exceeds his “elastic limit,” then he
soon becomes permanently injured thereby. It often
happens that an excessive amount of work is unavoidable,
but when it can be avoided it should be by those
who wish to preserve their health and strength.
In order to save themselves from great injuries,
runners and firemen should always act with the
greatest caution, and never rush carelessly into danger.
They should never adopt the principle of foolhardy
and thoughtless people, who by the consciousness
of continual danger fall into the habit of carelessly
“trusting to their luck,” etc. On the contrary,
they should always face the danger with their eyes
open and with the greatest conscientiousness. Many
try to show great courage by scorning the danger, and
some such even wish to meet a little in order to be
able to show their pluck. These should bear in mind
that they have a great responsibility laid upon them,
and that it is not alone their own well-being or life
which is at stake in case of any mishap, but that by
their careless behavior they may wound or kill the
helpless people who are committed to their care,
cause incalculable misery by robbing families of their
sole support and of their children; and bring great
sorrow and mourning to their fellow-men. The
thought of the curse and the despair of the survivors
may give sleepless hours even to a locomotive runner
who knows himself to have been without any fault
regarding an accident; how much more must it be
with him who cannot give himself this assurance?
There are not wanting instances in which the runner
who caused such an accident by his thoughtlessness,
driven to despair by his own heavily-burdened conscience,
went miserably to ruin.
Question 562.What requirements and duties should
every locomotive runner fulfill?
Answer. Every locomotive runner should fulfill the
following requirements and duties:
1. He should have an exact knowledge of the engine
intrusted to him, and a general knowledge of the
nature and construction of steam engines generally.
Likewise, he should be perfectly familiar with the
management of the boiler, the running of the engine,
and the way of keeping the working parts in good
condition; also, with the forms and peculiarities of
the line of road on which he runs, the rules which
govern the running of trains and with the signal system
adopted.
2. Health and bodily strength he must have in abundant
measure in his position, which is exhausting and
in which he is exposed to all sorts of weather.
3. He should have a good, plain common-school education,
and be ready at reading, writing and arithmetic.
4. He should always carry out exactly and cheerfully
the regulations of the service, or the instructions given
him by special orders from the officers over him.
5. Faithfulness, frankness and honesty, which characterize
an upright man in ordinary life, and also the
strictest temperance in the use of strong drink, he
should possess in a high degree in his very responsible
position.
6. He should have acquired a certain degree of skill
in putting together and taking apart locomotives, and
also in repairing separate parts of them. It is desirable
that he should always be present when his own
engine is taken apart, put together or repaired, in order
that he may acquire a thorough knowledge of its
condition and learn to understand properly the importance
of its various parts.
7. In caring for his engine he must preserve perfect
cleanliness and order, and in using fuel he must manifest
the greatest care and rigid economy.
8. Whenever there is danger, coolness and self-possession
are indispensably necessary, and any
thoughtlessness or recklessness is to be strictly
avoided.
9. Towards his superior officers his behavior should
be respectful and obliging; towards those under him,
patient and kindly, and at all times he should avoid
profanity and all intemperate language. He should
endeavor, as far as possible, to instruct the fireman
who accompanies him and make him familiar with
the construction and management of the engine, and
should see that he does his work strictly in accordance
with his instructions.
It is the fireman’s duty to follow the runner’s instructions
strictly, and in case of any sudden disability
of the runner he must stop the engine in accordance
with the instructions given him, and then give
the proper signals for help, until another runner arrives.
In the meanwhile the engine is to be kept at
a halt with all the usual precautions.
10. The runner should try to keep himself informed
of the progress and improvement of locomotives by
reading suitable hooks and technical periodicals, and
when possible acquire some skill in geometrical and
mechanical drawing, in order to accustom himself to
accurate work and sound and systematic thinking.
Question 563.What studies should mechanics, locomotive
runners and firemen take up, and what technical
books should they read?
Answer. As already stated, they should know how
to read and write their own language, and understand
arithmetic and have some knowledge of geography.
Every locomotive runner and fireman has a good deal
of spare time, a part of which he can devote to study,
and all of them, even if they have not had the advantage
of early education, could by industry and perseverance
acquire a knowledge of “reading, writing and
ciphering.” The assistance of a good teacher should
always be procured, if possible. With so much knowledge,
some book on natural philosophy can be read
to advantage, and then some book on mechanics. The
following list of books is given, which the student will
do well to read in the order in which they are named.
It should always be remembered, however, that the
mere buying of books contributes very little knowledge
to the owner. It is the reading and understanding
them which “increases knowledge.”
A Hand Book of the Steam Engine, by John Bourne; published by
Longmans, London; $2.00.
A Catechism of the Steam Engine, by John Bourne; published by
Longmans, London; $2.00.
Lessons in Elementary Physics, by Balfour Stewart; published by
Macmillan & Co., New York; $1.50.
Experimental Mechanics, by Prof. Ball; published by Macmillan &
Co., New York; $6.00.
The New Chemistry, by Prof. J. P. Cooke; published by Appleton &
Co., New York; $2.00.
Elementary Treatise on Heat, by Balfour Stewart; published by
Macmillan & Co., New York; $3.00.
Combustion of Coal, by C. Wye Williams; published by Lockwood &
Co., London; $1.20.
A Treatise on Steam Boilers, by Robert Wilson; published by Lockwood
& Co., London; $3.00.
Link-Valve Motion, by Wm. S. Auchincloss; published by D. Van
Nostrand, New York; $3.00.
The Conservation of Energy, by Balfour Stewart; published by Appleton
& Co., New York; $1.50.
Richards’ Steam Engine Indicator, by Charles T. Porter; published
by Longmans, London; $2.50.
Plates — PLATE IV. DIMENSIONS, WEIGHT, ETC., OF FOUR-WHEELED SWITCHING LOCOMOTIVE, By the Hinkley Locomotive Works, Boston, Mass. — Plate V. DIMENSIONS, WEIGHT, ETC., OF EIGHT-WHEELED “AMERICAN” LOCOMOTIVE By the Baldwin Locomotive Works, Philadelphia. — Plate vi. DIMENSIONS, WEIGHT, ETC., OF EIGHT-WHEELED “AMERICAN” LOCOMOTIVE By the Grant Locomotive Works, Paterson, N. J. — Plate vii. DIMENSIONS, WEIGHT, ETC., OF EIGHT-WHEELED “AMERICAN” LOCOMOTIVE BY THE Danforth Locomotive and Machine Co., Paterson, N. J. — Plate viii. DIMENSIONS, WEIGHT, ETC., OF EIGHT-WHEELED “AMERICAN” LOCOMOTIVE By the Mason Machine Works, Taunton, Mass. — Plate ix. DIMENSIONS, WEIGHT, ETC., OF EIGHT-WHEELED “AMERICAN” LOCOMOTIVE By the Hinkley Locomotive Works, Boston, Mass. — Plate x. DIMENSIONS, WEIGHT, ETC., OF TEN-WHEELED LOCOMOTIVE, By the Baldwin Locomotive Works, Philadelphia . — Plate xi. DIMENSIONS, WEIGHT, ETC., OF “MOGUL” LOCOMOTIVE, By the Baldwin Locomotive Works, Philadelphia . — Plate xii. DIMENSIONS, WEIGHT, ETC., OF “CONSOLIDATION” LOCOMOTIVE, BY THE Danforth Locomotive and Machine Co., Paterson, N. J. — Plate xiii. DIMENSIONS, WEIGHT, ETC., OF DOUBLE-END TANK LOCOMOTIVE, BY THE Rogers Locomotive and Machine Works, Paterson, N. J. — Plate xiv. DIMENSIONS, WEIGHT, ETC., OF DOUBLE-END TANK LOCOMOTIVE, BY THE Rogers Locomotive and Machine Works, Paterson, N. J. — Plate xv. DIMENSIONS, WEIGHT, ETC., OF IMPROVED TANK LOCOMOTIVE, DESIGNED BY M. N. Forney, 73 Broadway, New York . — Plate xvi. DIMENSIONS, WEIGHT, ETC., OF Double-truck Narrow-gauge Tank Locomotive , By the Mason Machine Works, Taunton, Mass. — Plate xvii. DIMENSIONS, WEIGHT, ETC., OF DOUBLE-TRUCK TANK FREIGHT LOCOMOTIVE, By the Mason Machine Works, Taunton, Mass. — Plate xviii. DIMENSIONS, WEIGHT, ETC., OF DOUBLE-END LOCOMOTIVE, By the Grant Locomotive Works, Paterson, N. J. — Plate xix. DIMENSIONS, WEIGHT, ETC., OF LOCOMOTIVE FOR THE N. Y. ELEVATED R. R. Designed by D. W. Wyman, Superintendent.
Gauge of Road
4 ft. 8¹⁄₂ in.
Number of Driving-Wheels
4
Number of Front Truck-Wheels
None.
Number of Back Truck-Wheels
None.
Total Wheel Base
6 ft. 9 in.
Distance between Front and Back Driving-Wheels
6 ft. 9 in.
Total Weight of Locomotive in working order
48,000 lbs.
Total Weight on Driving-Wheels
48,000 lbs.
Diameter of Driving-Wheels
50 in.
Diameter of Truck-Wheels
None.
Diameter of Cylinders
15 in.
Stroke of Cylinders
22
Outside Diameter of smallest Boiler ring
44³⁄₄ in.
Size of Grate
3 × 3²⁄₃ ft.
Number of Tubes
121
Diameter of Tubes
2 in.
Length of Tubes
10¹⁄₂ ft.
Square Feet of Grate surface
11
Square Feet of Heating surface in Fire-Box
71
Square Feet of Heating surface in Tubes
580
Total Feet of Heating surface
651
Exhaust Nozzles—single or double
Double.
Diameter of Nozzle
2³⁄₄ in.
Size of Steam Ports
10 × 1¹⁄₄ in.
Size of Exhaust Ports
2¹⁄₄ in.
Throw of Eccentrics
4¹⁄₂ in.
Outside Lap of Valve
³⁄₄ in.
Inside Lap of Valve
None.
Size of Main Driving-axle Journal
6¹⁄₂ × 7 in.
Size of other Driving-axle Journal
6¹⁄₂ × 7 in.
Size of Truck-axle Journal
None.
Diameter of Pump Plunger
1⁷⁄₈ in.
Stroke of Pump Plunger
22 in.
Capacity of Tank
1,200 gallons.
Plate IV.
FOUR-WHEELED SWITCHING LOCOMOTIVE, BY THE HINKLEY LOCOMOTIVE WORKS, BOSTON, MASS.
Scale, ¹⁄₈ in. = 1 ft.
Gauge of Road
4 ft. 8¹⁄₂ in.
Number of Driving-Wheels
4
Number of Front Truck-Wheels
4
Number of Back Truck-Wheels
None.
Total Wheel Base
21 ft. 9 in.
Distance between centres of Front and Back Driving-Wheels
96 in.
Total Weight of Locomotive in working order
65,000 lbs.
Total Weight on Driving-Wheels
42,000 lbs.
Diameter of Driving-Wheels
60³⁄₄ in.
Diameter of Truck Wheels
28 in.
Diameter of Cylinders
16 in.
Stroke of Cylinders
24 in.
Outside Diameter of smallest Boiler Ring
48 in.
Size of Grate
65 × 34¹⁄₂ in.
Number of Tubes
144
Diameter of Tubes
2 in.
Length of Tubes
10 ft. 11 in.
Square Feet of Grate surface
15.5
Square Feet of Heating surface in Fire-Box
100.6
Square Feet of Heating surface in Tubes
825.4
Total Feet of Heating surface
926
Exhaust Nozzles—single or double
Double.
Diameter of Nozzle
2³⁄₄ to 3¹⁄₄ in.
Size of Steam Ports
1¹⁄₄ × 15 in.
Size of Exhaust Ports
2¹⁄₂ × 15 in.
Throw of Eccentrics
5¹⁄₂ in.
Outside Lap of Valve
³⁄₄ in.
Inside Lap of Valve
¹⁄₃₂ in.
Size of Main Driving-axle Journal
7 in. dia. × 8 in.
Size of other Driving-axle Journal
7 in. dia. × 8 in.
Size of Truck-axle Journal
4¹⁄₂ × 7¹⁄₂ in.
Diameter of Pump Plunger
2 in.
Stroke of Pump Plunger
24 in.
Capacity of Tank
2,000 gallons.
Plate V.
EIGHT-WHEELED “AMERICAN” LOCOMOTIVE, BY THE BALDWIN LOCOMOTIVE WORKS, PHILADELPHIA.
Scale, ¹⁄₈ in. = 1 foot.
Gauge of Road
4 ft. 8¹⁄₂ in.
Number of Driving-Wheels
4
Number of Front Truck-Wheels
4
Number of Back Truck-Wheels
None.
Total Wheel Base
21 ft. 9 in.
Distance between centres of Front and Back Driving-Wheels
8 ft.
Total Weight of Locomotive in working order
62,000 lbs.
Total Weight on Driving-Wheels
42,000 lbs.
Diameter of Driving-Wheels
61 in.
Diameter of Truck-Wheels
28 in.
Diameter of Cylinders
16 in.
Stroke of Cylinders
24 in.
Outside Diameter of smallest Boiler Ring
48 in.
Size of Grate
60 × 34 in.
Number of Tubes
140
Diameter of Tubes
2 in.
Length of Tubes
11 ft.
Square Feet of Grate surface
14
Square Feet of Heating surface in Fire-Box
98
Square Feet of Heating surface in Tubes
805
Total Feet of Heating surface
903
Exhaust Nozzles—single or double
Double.
Diameter of Nozzle
3¹⁄₄ to 3³⁄₄ in.
Size of Steam Ports
1¹⁄₄ × 14 in.
Size of Exhaust Ports
2¹⁄₂ × 14 in.
Throw of Eccentrics
5 in.
Outside Lap of Valve
³⁄₄ in.
Inside Lap of Valve
None.
Size of Main Driving-axle Journal
6¹⁄₂ dia. × 7³⁄₄ in.
Size of other Driving-axle Journal
6¹⁄₂ dia. × 7³⁄₄ in.
Size of Truck-axle Journal
4¹⁄₂ dia. × 8 in.
Diameter of Pump Plunger
2 in.
Stroke of Pump Plunger
24 in.
Capacity of Tank
2,000 gallons.
Plate VI.
EIGHT-WHEELED “AMERICAN” LOCOMOTIVE, BY THE GRANT LOCOMOTIVE WORKS, PATERSON, N. J.
Scale, ¹⁄₈ in. = 1 ft.
Gauge of Road
4 ft. 8¹⁄₂ in.
Number of Driving-Wheels
4
Number of Front Truck-Wheels
4
Number of Back Truck-Wheels
None.
Total Wheel Base
21 ft 2 in.
Distance between centres of Front and Back Driving-Wheels,
7 ft. 9 in.
Total Weight of Locomotive in working order
60,200 lbs.
Total Weight on Driving-Wheels
38,350 lbs.
Diameter of Driving-Wheels
5 ft. 7⁵⁄₈ in.
Diameter of Truck-Wheels
2 ft. 6 in.
Diameter of Cylinders
15 in.
Stroke of Cylinders
24 in.
Outside Diameter of smallest Boiler Ring
3 ft. 10 in.
Size of Grate
56 × 34¹⁄₂ in.
Number of Tubes
136
Diameter of Tubes
2 in.
Length of Tubes
11 ft.
Square Feet of Grate surface
13.5
Square Feet of Heating surface in Fire-Box
86
Square Feet of Heating surface in Tubes
775
Total Feet of Heating surface
861
Exhaust Nozzles—single or double
Double.
Diameter of Nozzle
2³⁄₄ in.
Size of Steam Ports
1¹⁄₄ × 13¹⁄₂ in.
Size of Exhaust Ports
2¹⁄₂ × 13¹⁄₂ in.
Throw of Eccentrics
5¹⁄₂ in.
Outside Lap of Valve
⁷⁄₈ in.
Inside Lap of Valve
¹⁄₈ in.
Size of Main Driving-axle Journal
6¹⁄₂ in.
Size of other Driving-axle Journal
6¹⁄₂ in.
Size of Truck-axle Journal
4¹⁄₂ in.
Diameter of Pump Plunger
2¹⁄₈ in.
Stroke of Pump Plunger
24 in.
Capacity of Tank
1,800 gallons.
Plate VII.
EIGHT-WHEELED “AMERICAN” LOCOMOTIVE, BY THE DANFORTH LOCOMOTIVE AND MACHINE CO., PATERSON, N. J.
Scale, ¹⁄₈ in. = 1 ft.
Gauge of Road
4 ft. 8¹⁄₂ In.
Number of Driving-Wheels
4
Number of Front Truck-Wheels
4
Number of Back Truck-Wheels
None.
Total Wheel Base
22 ft.
Distance between centres of Front and Back Driving-Wheels
Air, admission of to fire-box, 380; control of supply of, 384; forces of,
8; method of admitting to the fire-box, 382; pressure of, 8,
9; quantity necessary for combustion, 381, 388; quantity needed for
dilution of gases, 389; quantity to be admitted through the grate and above the fire, 391;
weight of, 8.
Combustion, 365; air required for, 380, 388; chemical process
of, 379; effect on of enlarging the grate, 392; how explained, 370;
in locomotive fire-box, 377; intensity of, 393; in tubes, 386;
products of, 378; rate of, 73, 365; total heat of,
380, 393; when complete, 373.
Compression, 44, 221; calculation of, 243; effected by,
228; effect of, 247; line or curve of, 236.
Driving-wheels, 70, 268; action of, 323; adhesion of,
62, 319; breaking of, 523; construction of,
285; distance between, 68; effect of their size on combustion and evaporation,
424; friction of, 62, 319; how fastened, 288;
motion of around curves, 284; relation between size of and that of boiler, 425; size of,
68, 413, 425; weight on, 69.
Eccentric, 6; effect of throw of, 252, 255; how set,
182, 528; motion how communicated to valve, 185; motion same as
that of crank, 31; slipping of, 526, 528; throw of,
31, 251; with varying lap, 258.
Friction, 358; depends on, 358; co-efficient of, 359; effect of
pressure and velocity of surfaces on, 361; effect of area of surfaces in contact, 364; law
of, 363; of wheel flanges, 281; of wheels, 62,
319.
Locomotive, 62; advance of, 323; capacity of, 421; cleaning and
repairing of, 505; cost of operating, 448; different kinds, 427;
dimensions of, 68, 429; escape of, 509, 511;
experiments with, 450; general description of, 62; how turned around,
455; inspection of, 461; list of parts of, 69; number of miles run to
a ton of coal, 449; principal parts of, 62; proportions of, 412;
resistance of, 62; speed of, 419; starting of, 480; weight of,
67.
Slide-valve, 6, 30; advance of, 38; conditions which it
must fulfill, 30; disadvantages of first form of, 37; first form of,
30; how made steam tight, 169; inspection of, 472; lap of,
40; middle position of, 184; motion of modified by the proportions of link motion,
248; oiling of, 169, 492; proportions of, 260;
setting of, 264; travel of, 38.
Truck, 268; construction of, 314; effect of on movement of locomotive around curves,
273; for tender, 356; lateral motion of, 317; resistance to rolling,
280; use of, 269; with single pair of wheels, 271,
430.
Inconsistencies in spelling, lay-out, hyphenation, etc. have been retained, except as mentioned under Changes below.
Some reference letters’ case in the text does not correspond to that shown in the illustration, and some of the reference
letters are used inconsistently in different illustrations; this has not been rectified unless mentioned below. The not
always numerical order of the illustrations in this e-text is the order of the source document. Depending on the hard- and software used to read this text and their
settings, not all elements may display as intended. The scale as indicated in the illustrations in this e-text is not necessarily correct.
Several characters as used in this text are used to represent the shape of the symbol or letter rather than the symbol’s (e.g., ⟂) or letter’s
(e.g., ~U~) actual meaning.
Page 47, ... a spiral spring, s s, fig. 31, which is compressed ...: the letters s are not visible in the illustration (the spring is).
Page 52, ... if we construct a scale S, S, fig. 38, ...: the printing quality of the source document was not sufficient to
make this entirely visible in the illustration; the text and fig. 39 may provide clarity. The parts that were legible have been enhanced.
Page 77: Fig. 41 contains different reference letters h: two in the smoke stack (left-hand side of the illustration),
one underneath the steam whistle. Both are referenced in the text.
Page 102, ... the distance d f will then be the centre ...: one or more words may be missing (... which will then be ... or similar).
Page 154, ... with two handles, l, l, fig. 71, which are raised ...: reference letters l do not occur in the illustration
(nor are they listed in the parts list following the illustration).
Page 166, Fig. 93: the right-most reference letter is an upside-down W, not an M.
Page 181, ... and the other two the reverse way: possibly an error for ... and the other the reverse way.
Page 258, caption with fig. 145: Scale ³⁄₁₆ in. = 1 foot is probably an error for Scale ³⁄₁₆ in. = 1 inch.
Page 269, ... and y, plate II, and fig. 40, the centre-pin ...: the centre-pin is indicated by Y in Plate II.
Page 337, The running-boards are planks, i i, plate I, ...: the reference letters i i are not visible in Plate I.
Page 430, Sentence starting For this reason a truck consisting of a single pair of wheels, ...: as printed in the source document; some text may be missing.
Page 448/449, Table and paragraph starting From this table it will be seen ...: probably the last two columns of the table list
decimal fractions rather than percentages (e.g., fuel is probably 0.3 of operating costs of locomotives rather than 0.3%).
Page 544: Part XL should have been called Part XXX.
Appendices: unless mentioned under Changes below the tables are given here as printed, although they may contain (minor) errors.
Changes made
Footnotes and illustrations have been moved out of text paragraphs. Some of the illustrations have been rotated. Figure numbers and scale indicators have been
removed from within some illustrations and have been transcribed as (top or bottom) captions.
Where they were missing, periods have been added to illustration captions. Numbered questions have (where relevant)
been standardised to end in a question mark. Reference letters in the text have been standardised to italics.
Some obviously missing punctuation has been inserted; some minor obvious typographical errors were
corrected silently. In some tables and lists ditto marks have been replaced with the dittoed text.
Page iv: Die Schule des Locomotivfuhrers ... changed to Die Schule des Locomotivführers ....
Page xvi: ... as shown in the sections of the apple at A and B. changed to ... as shown in the sections of the apple at C and D.
Page 1: The steam, if admitted at c ... changed to The steam, if admitted at C ....
Page 40: ... those portions of the face h, i, and p, q, which cover the steam-ports, ... changed to ... those portions of the
face h, i, and h′, q, which cover the steam-ports ....
Page 56: ... conditions which were used in the answer to Question 60 ... changed to ... conditions which were used in the answer to Question 57 ....
Page 58: It was shown in answer to Question 56 ... changed to It was shown in answer to Question 57 ....
Page 102: ... we will step off the distance d f f ... changed to ... we will step off the distance d f ....
Page 111: ... (shown also in fig. 43,) ... changed to ... (shown also in fig. 40,) ....
Page 129: first comma deleted from a, a′, Heater Pipe.
Page 135: Fig. 74: reference letter J changed to j.
Page 162: ... flanges, f f, cast on the pipes. changed to flanges, f, f, cast on the pipes.
Page 165: ... _heads_, A and _B_, ... changed to ... _heads_, _A_ and _B_, ....
Page 176: ... the tops guides are usually ... changed to ... the top guides are usually ....
Page 179: ... the journals of the coupling-rods, the brasses at m, m, ... changed to ... the journals of the coupling-rods, the brasses at n, n, ....
Page 195: Thus the line -o -o, ... changed to Thus the line -0 -0 ....
Page 216, table, row 4, column Point of release, Backward stroke 20¹¹⁄₁₅ changed to 20¹¹⁄₁₆.
Page 220: ... the slide-valve and ink motion? changed to ... the slide-valve and link motion?
Page 234 and 236: The first illustration with caption Fig. 136 has been renumbered Fig. 136a, the second one Fig. 136b.
Page 236, Fig. 136b: reference letter e (top centre) changed to c.
Page 261: The reverse-rod l′ k, which connects the lever with the vertical arm k ... changed to
The reverse-rod e k, which connects the lever with the vertical arm k ....
Page 281: ... if two pairs of wheels, a, a′, b, b′, fig. 151, ... changed to ... if two pairs of wheels, a a′, b b′, fig. 151, ....
Page 292: ... a heavy timber, called a bumper-timber, E E, plates I, II and III, ... changed to ... a
heavy timber, called a bumper-timber, E′ E′, plates I, II and III, ....
Page 297: These plates are of different lengths, as shown at B, B, in fig. 169, ... changed to These
plates are of different lengths, as shown at B, B′, in fig. 169, ....
Page 308, answer to question 299: references to Fig. 178 changed to Fig. 177 (three times).
Page 327: ... the end of a longer lever E G′ B, fig. 192, ... changed to ... the end of a longer lever E G B, fig. 192, ....
Page 337: The hand-rails, m m′ m′, are brass or iron pipes ... changed to The hand-rails,
m′ m′ m′, are brass or iron pipes ....
Page 345: closing quote mark inserted after formula.
Page 346, first formula: 1,266 changed to 1.266 as elsewhere.
Page 366: the source has two footnote anchors for a single footnote; the footnote has been copied.
Page 423: ... 649,725 units of heats, ... changed to ... 649,725 units of heat, ....
Page 432, answer to question 435: quote marks inserted around Consolidation as elsewhere.
Page 499, footnote 111: Katechismus der Einrichtung und Betriebes der Locomtive changed to Katechismus der Einrichtung und des Betriebes der Locomotive.
Page 544, footnote119: Katechismus der Einrichtung und Betriebes der Locomotive changed to Katechismus der Einrichtung und des Betriebes der Locomotive.
Page 561, Plate VIII: Scale, ¹⁄₈ in. = ft. changed to Scale, ¹⁄₈ in. = 1 ft.
Appendices: chapter headings Appendix I, Appendix II, Appendix III and Appendix IV have been inserted.
Index: some page numbers were corrected. Minor spelling differences between the text and the index have not been changed.